


Highlights
What are the main findings?
- Twelve variants of twisted copper-based conductive threads were successfully fabricated using cotton and polyester substrates with carbon paste derived from e-waste dry cell batteries.
- The optimized thread (C3C4A) achieved a very low electrical resistance of 0.0164 ± 0.0001 Ω/cm, comparable to or lower than several commercial conductive yarns.
- The developed threads maintained stable electrical performance under bending, twisting, and repeated wash–dry cycles.
What are the implications of the main finding?
- The results demonstrate a low-cost and environmentally sustainable approach for producing conductive threads using recycled e-waste materials.
- These threads can be integrated into flexible fabric circuits, wearable sensors, and smart textile systems, supporting practical applications such as textile-based electronics and smart garments.
Abstract
Conductive thread is an integral aspect of smart textiles in the domain of electronic textiles (e-textiles). This study unveils the development of twelve distinct variants of conductive threads using the twisting method: the fusion of copper filament with cotton and polyester threads. The threads are coated with a carbon paste solution enriched with dissolved sea salt. The carbon paste is obtained from non-functional dry cell batteries, conventionally categorized as hazardous electronic waste (e-waste), which underscores an economically viable and environmentally sustainable approach. Experiments proved that each variant demonstrates minimal electrical resistance. The lowest resistance, 0.0164 ± 0.0001 Ω/cm, was achieved by Carbon-Coated Cotton Twisted Copper Thread-II. Comparative evaluation with commercially available conductive threads, including Bekaert Bekinox® VN type (12/1x275/100z), indicated comparable or moderately lower resistance values for the developed copper-based threads. Mechanical–electrical stability under bending, twisting, and wash–dry cycles confirmed consistent conductive performance with minimal resistance variation. Practical demonstrations further validated the integration of the threads into fabric-based flexible circuits and wearable electronic systems. These findings demonstrate that twisted copper-based conductive threads derived from sustainable coating materials provide a promising alternative for smart textile and wearable electronic applications. Future research should focus on scalable fabrication, enhanced coating fixation, and long-term durability assessment.
1. Introduction
The term ‘smart textile’ denotes fabrics capable of sensing their surroundings and responding appropriately to external factors [1,2]. These innovative textiles seamlessly integrate electronic components into fabric structures, facilitating a wide array of functionalities including sensing, communication, and actuation [3]. In the past decades, various efforts have been made to develop electrically conductive textiles and optimize their performances [4]. The conductive thread serves as the fundamental building block for creating flexible and interconnected circuits within fabric substrates [5]. The development of conductive threads with enhanced functionality, conductivity, flexibility, and environmental sustainability is essential for advancing the capabilities and applications of smart textiles.
Conventional conductive threads, including metal-coated fibers and conductive yarns, have been the primary materials used in smart textiles for conducting electricity [5]. Conductive thread commonly found in the market often features a solid metal wire, like copper or stainless steel, or a non-conductive thread coated with a thin layer of metal, typically silver, with a thickness of approximately 1 micron. Due to their tendency to become hard and brittle and their susceptibility to shattering after repetitive bending, these solutions become inferior [6]. Other coatings, for instance, conductive polymers [7], graphene flakes, and carbon nanotubes (CNTs) [8,9,10], have lately been proposed as viable replacements for flexible conductive threads. Graphene coating is often expensive and complex, which limits large-scale production, and its conductivity depends on factors like solvent type and annealing temperature. Furthermore, it has been demonstrated that conductive thread can be produced by coating the thread using metallic nanoparticles, for example, gold (Au), silver (Ag) or platinum (Pt) [1,11,12,13,14]. However, their comparatively high cost can have an adverse effect on end-user affordability. Nanostructured polymers that are conductive or conjugated are ideal for bio-sensing applications [14,15]. In 2004, Atwa et al. demonstrated the fabrication of conductive threads using nylon and cotton coated with silver nanowires and achieved a resistance of 0.8 Ω/cm by varying the nanowire density [16]. Fahad Alhashmi Alamer and colleagues developed the threads by the drop-casting method and calculated the least resistance at 0.0072 Ω, in contrast to SWCNTs and PEDOT:PSS at 0.0211 Ω and 0.0528 Ω respectively [17]. In addition, using 6 mL of graphene dispersed in ethanol and treated at 78 °C resulted in a remarkably low minimum electrical resistance of 0.0127 Ω/cm [5]. Recent advances have enabled flexible conductors from 2D materials like graphene, integrated into electronic skins and textiles [18]. Silver is the most prevalent metal due to its superior conductivity, affordability compared to gold or platinum, and overall stability in air. Silver nanoparticles are more expensive than copper ones and can accumulate in soil and water. This poses risks to ecosystems and human health when they are released during production or disposal. The copper (Cu) filament is a cost-effective and high-conductive material. Copper has been extensively researched as an alternative to silver owing to its significantly lower cost, approximately 1% of that of silver, and high electrical conductivity, which is only about 6% less than that of silver [19]. Compared to the electrical resistance of metals, which is approximately 10−5 Ω/cm, insulators exhibit a much higher resistance, typically around 1012 Ω/cm [20].
The growing global focus on environmental sustainability has spurred efforts to explore and create innovative materials by recycling waste, aiming to reduce reliance on non-renewable resources and minimize environmental harm from waste generation [21]. Many researchers have developed textiles using waste materials, as the increasing amount of non-biodegradable waste poses a significant threat to environmental sustainability. Recently, disposed electrical and electronic equipment (EEE) has been identified as hazardous waste [22]. Lockdowns and remote work, increasing electronics demand during the COVID-19 pandemic, have exacerbated worldwide electronic waste (e-waste) [23]. Toxic components and heavy metals in e-waste, which totalled 53.6 million metric tons in 2019, are expected to reach 120 million by 2050. These substances pose a significant threat to human and environmental health [24]. Another important fact is that most wearable microelectronic devices are rigid, even though some are integrated into flexible textiles. As a result, the practical applications of textile-based wearable systems are still in the early stages [25].
This study aims to address the challenges prevalent in electronic textiles by developing low-resistance, cost-effective conductive threads and formulating eco-friendly coating agents from e-waste. Through systematic experimentation, the research endeavors to optimize the fabrication processes with a particular emphasis on examining the connection between the selection of solvents and the electrical characteristics of conductive textile threads.
2. Materials and Methods
2.1. Materials
This research used commercially available cotton threads (40/3) and polyester threads (40/2). Each copper filament obtained from copper wire was capable of conducting a current of 31.81 mA and had a density of 0.4262 mg/cm. Copper filament had an average diameter of approximately 90 μm, determined from the AWG 39 specification and also measured using a digital micrometer. Carbon paste was extracted from a non-operational dry-cell battery, and sodium chloride (NaCl), commonly known as sea salt, was obtained from seawater. One of the most important considerations is that all types of commercially available local materials and chemicals were sourced from Dhaka, Bangladesh.
2.2. Preparation of Coating Solution
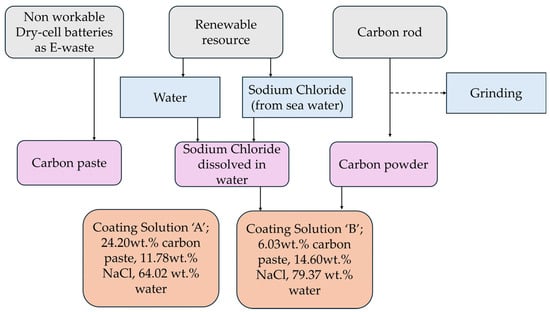
The procedure for preparing the coating solutions or agents is illustrated in Figure 1. Two distinct coating solutions (A and B) were prepared using the following procedure: Solution ‘A’ was prepared by first dissolving 1.84 g of NaCl in 10 mL of water (H2O). This NaCl solution was then mixed with 3.78 g of carbon paste and stirred thoroughly to ensure uniform dispersion. The final composition of the mixture was 24.20% carbon paste, 11.78% NaCl, and 64.02% water by weight. Solution ‘B’ was prepared with 0.76 g of carbon powder obtained by grinding a carbon rod. Afterward, 1.84 g of NaCl was mixed with 10 mL of water and thoroughly stirred with carbon powder. The content of carbon powder, NaCl, and water were 6.03%, 14.60%, and 79.37% respectively.
Figure 1.
Procedure for preparation of coating solutions.
2.3. Preparation of Conductive Threads
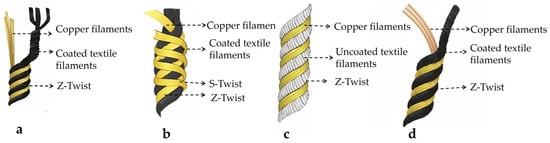
In this research, twelve types of conductive threads were produced, encompassing both coated and uncoated variations. All types of threads were made by hand twisting process, including multi-filament twisted (Figure 2a), double twisted (Figure 2b), and Z-twisted structures (Figure 2c,d).
Figure 2.
Twisting techniques: (a) Multi-filament twisted structure. (b) Double twisted structure. (c) Z-twisted non-coated structure. (d) Z-twisted coated structure.
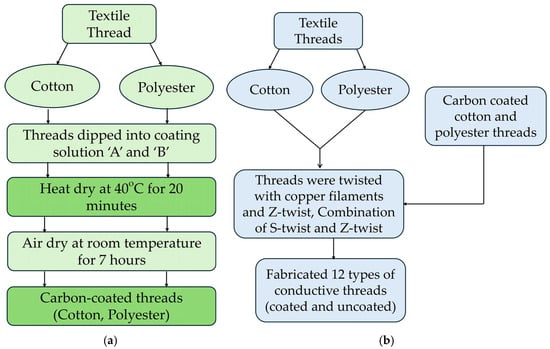
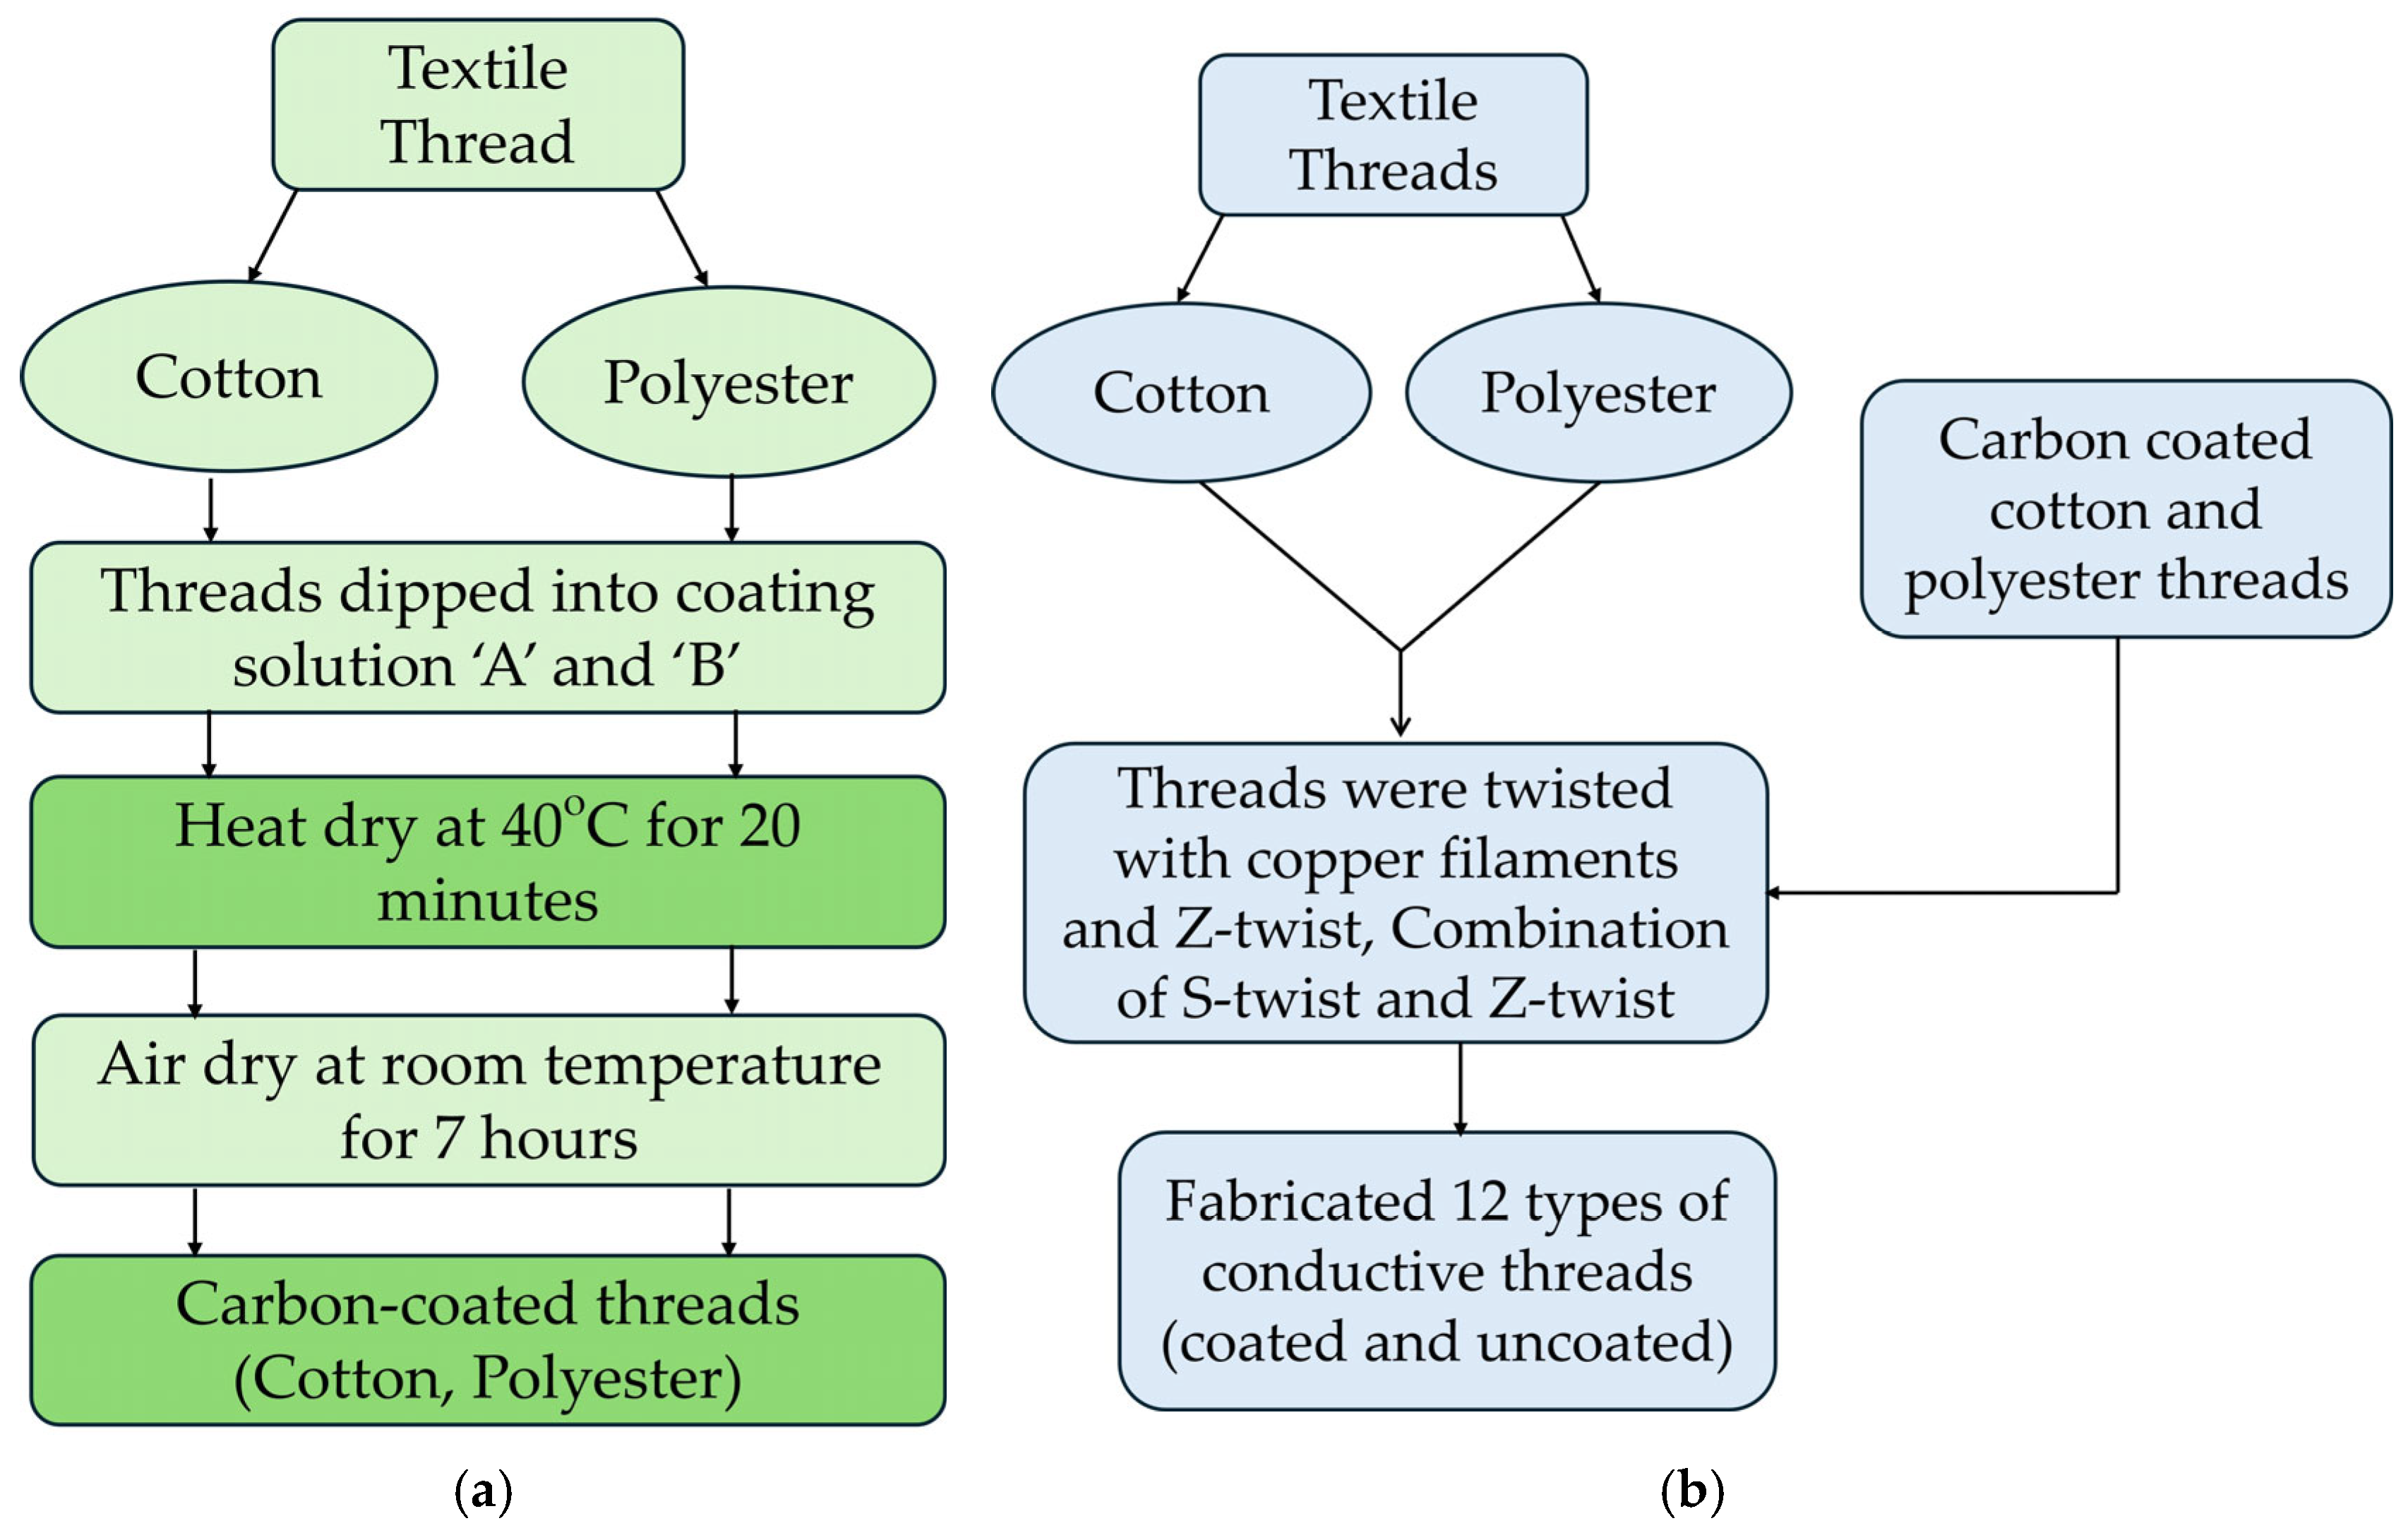
The fabrication process of conductive threads involved the utilization of two distinct coating agents, denoted as Solution ‘A’ and Solution ‘B’. Initially, a total of 190.5 cm each of polyester and cotton threads were dipped into Solution A, followed by subjecting them to a heat dryer set at 40 °C for a duration of 20 min. Subsequently, the treated threads were allowed to undergo thorough drying at room temperature for a period spanning 7 h. Figure 3a demonstrates the coating technique applied to conductive threads. In a parallel procedure, another batch of identical dimensions (190.5 cm), comprising polyester and cotton threads, was similarly dipped in Solution B, with identical procedural steps encompassing heat drying at 40 °C for 20 min. Subsequently, the treated threads were also allowed to undergo thorough drying under ambient conditions for a period spanning 7 h. Figure 3b depicts the twisting procedure for the conductive thread. The cotton thread comprised three plies, and the polyester thread had two plies. Table 1 provides details of the number of plies, twisting method and coating agent (solution) used for different conductive threads.
Figure 3.
Schematic illustration of (a) the coating process and (b) the twisting process used for fabricating the conductive threads.
Table 1.
Fabrication details of conductive threads showing number of plies, twisting method and coating agent used.
2.4. Characterization and Performance Evaluation
Yarn count was determined using the indirect English cotton count system (Ne). A known length of yarn was measured and weighed under standard laboratory conditions, and the count was calculated using
where L is the yarn length in yards, and W is the mass in pounds. Measurements were performed in triplicate, and results are reported as mean ± standard deviation. Electrical resistance per unit length was measured using a precision digital multimeter model UNI-T UT33D+ under controlled laboratory conditions. Conductivity was calculated from the measured resistance values. All the measurements were repeated three times, and mean values with standard deviation are reported. Surface morphology was examined using a FEI Quanta 250 scanning electron microscope operated at an accelerating voltage of 15 kV. Images were acquired at magnifications ranging from approximately 500× to 1000×. The thread samples were cut into small segments and mounted on aluminum stubs using conductive carbon tape. No sputter coating was applied, as the copper filaments and carbon coating provided sufficient electrical conductivity to prevent charging during imaging.
A stir washing test was conducted to evaluate the laundering durability of coated and uncoated conductive threads by simulating mechanical agitation in a domestic washing process, following a similar durability evaluation approach reported for Cu-Ag nanonet conductive textiles [4]. Each thread sample was immersed in tap water containing detergent and stirred at 500 rpm for 10 min at room temperature. The samples were then removed and dried at 50 °C for 30 min to complete one wash–dry cycle. This cycle was repeated ten times. Electrical resistance per unit length was measured after each cycle. Mechanical and electrical stability were further evaluated under repeated bending and twisting deformation for 500 cycles, consistent with previously reported flexibility testing of Cu-Ag nanonet-based conductive threads [4]. In the bending test, the samples were subjected to cyclic deformation at an angle of 150°. In the twisting test, the samples were rotated to 360° per cycle. Electrical resistance per unit length was continuously monitored during deformation using a precision multimeter to assess resistance variation under mechanical stress. All the measurements were conducted under identical laboratory conditions and performed in triplicate. Statistical analysis was conducted using a paired t-test to evaluate resistance changes before and after cyclic deformation. The significance level of p <0.05 was considered statistically significant.
3. Results and Discussion
3.1. Surface Morphology Analysis of Conductive Threads Using Scanning Electron Microscopy (SEM)
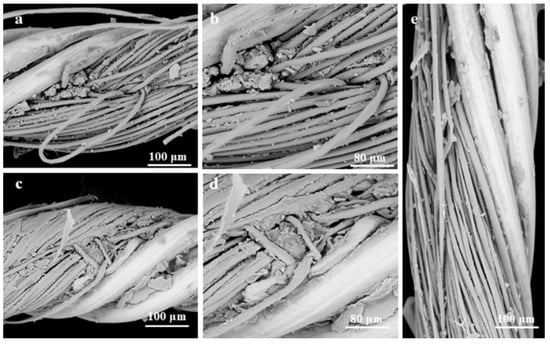
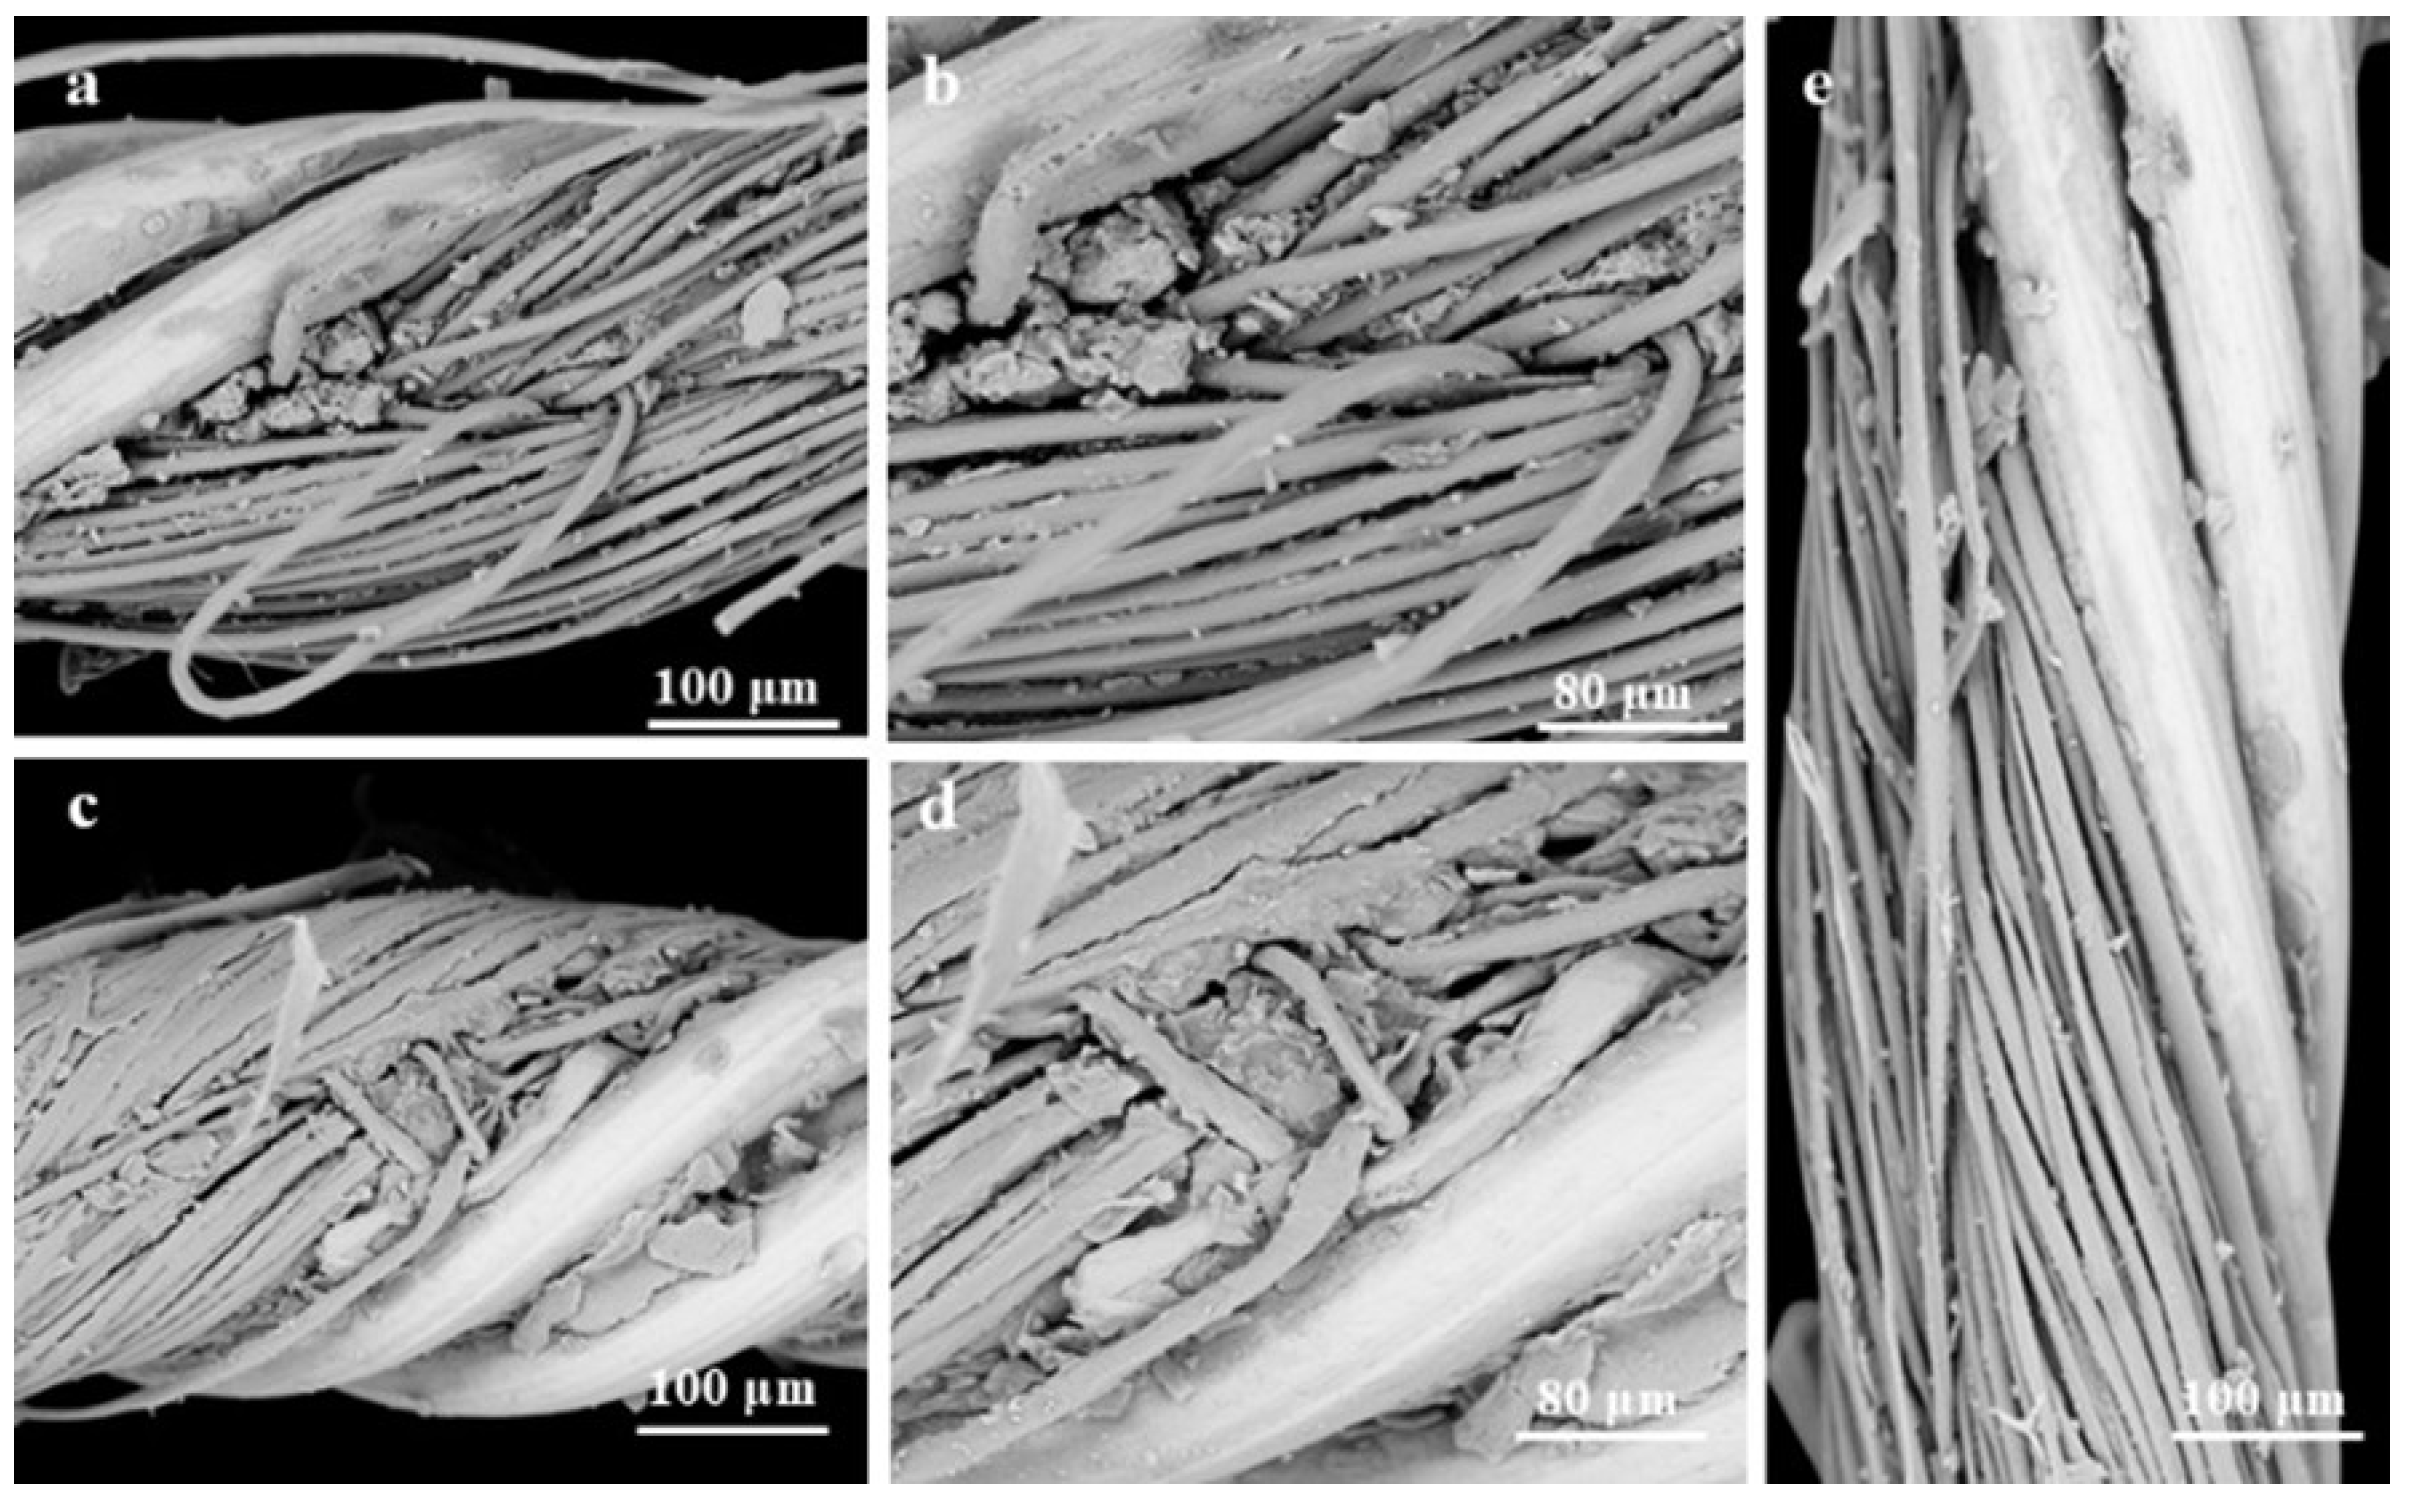
Scanning electron microscopy was conducted to examine the surface morphology of the threads P2C4A (Thread 3), C3C4A (Thread 7), and C3C2n (Thread 8). Representative micrographs are shown in Figure 4. Thread 3 (Figure 4a) exhibits a clearly defined twisted structure consisting of polyester fibers integrated with copper filaments. The corresponding higher-magnification image (Figure 4b) reveals limited and non-uniform carbon coating on the polyester fibers. The relatively smooth and less porous surface of polyester appears to restrict coating adhesion and penetration. In contrast, Thread 7 (Figure 4c) demonstrates a more pronounced coating presence. The twisted configuration of cotton and copper filaments remains visible beneath the carbon layer. Figure 4d presents a higher-magnification view of the same region shown in Figure 4c, illustrating that the carbon paste effectively covers a larger number of cotton fibers and partially fills the inter-fiber spaces. This behavior can be attributed to the higher absorbency and porous structure of cotton fibers, which promotes improved coating uptake compared to polyester. Thread 8, shown in Figure 4e, does not contain a carbon coating layer. The micrograph indicates a well-defined twisting structure of cotton and copper filaments, along with the presence of surface wax residues. Despite the absence of an external conductive coating, the integrated copper filaments provide continuous conductive pathways along the thread structure. The SEM observations indicate that fiber type significantly influences coating distribution and inter-fiber coverage. Cotton-based threads exhibit improved coating penetration and interconnection, which may enhance electrical pathway formation. These structural characteristics are consistent with the electrical performance trends observed in subsequent conductivity and stability analyses.
Figure 4.
SEM analysis of surface morphology of developed conductive threads: (a) SEM image of P2C4A. (b) Higher-magnification image of P2C4A showing limited and non-uniform carbon coating on polyester fibers. (c) SEM image of C3C4A. (d) Higher-magnification image of C3C4A showing that carbon paste covers a larger number of cotton fibers and partially fills the inter-fiber spaces. (e) SEM analysis of C3C2n.
3.2. Electrical Resistance and Thread Count Measurement
The electrical resistance (R) and thread count of the twelve developed conductive threads were measured, and the results are summarized in Table 2. The linear density was expressed using the English cotton count (Ne), where a lower Ne value indicates a coarser thread and a higher Ne value indicates a finer thread [26].
Table 2.
Measured resistance and thread count of the developed conductive threads.
Several threads with a count of 3 Ne exhibited consistently low resistance values of approximately 0.0197 ± 0.0001 Ω/cm. These include P2C4n, C3C4n, P2C4A, C3C4n-DT, P2C4n-DT, and C3C3n. Among the 3 Ne threads, C3C4A showed the lowest resistance of 0.0164 ± 0.0001 Ω/cm, indicating improved electrical continuity due to the combined effect of cotton fiber structure and carbon coating.
Threads with higher Ne values generally showed increased resistance. C3C2n and P2C3n, both with a count of 3.6 Ne, exhibited resistance values of 0.0470 ± 0.0001 Ω/cm and 0.0230 ± 0.0001 Ω/cm, respectively. The finest sample, C3C1n with a count of 4.5 Ne, demonstrated a resistance of 0.0459 ± 0.0001 Ω/cm. The carbon-coated cotton twisted copper threads with intermediate counts, namely C3C3A (3.18 Ne) and C3C3B (3.37 Ne), showed resistance values of 0.0250 ± 0.0001 Ω/cm and 0.0273 ± 0.0001 Ω/cm, respectively.
These results indicate that coarser conductive threads generally exhibit lower electrical resistance due to their larger effective cross-sectional area, which facilitates improved current flow [27]. While thread count influences resistance, the type of conductive material, fiber substrate, coating presence, and filament arrangement play a more significant role in determining electrical performance. Finer threads may offer advantages in suitability for wearable sensing applications, whereas coarser threads provide lower resistance and enhanced electrical conductivity for power and signal transmission applications.
To further investigate the influence of structural variables on electrical performance, direct comparisons were made among the samples differing only in coating, structure, or copper filament content. Comparing P2C4n and P2C4A shows identical resistance values (0.0197 ± 0.0001 Ω/cm), indicating that carbon coating A does not significantly affect conductivity for polyester-based threads, likely due to limited coating penetration associated with the smoother polyester surface. In contrast, the cotton-based samples exhibit a measurable coating effect, with C3C4A showing a reduced resistance of 0.0164 ± 0.0001 Ω/cm compared to 0.0197 ± 0.0001 Ω/cm for C3C4n. This corresponds to an approximate 17% decrease and can be attributed to enhanced coating uptake and inter-fiber bridging facilitated by the porous cotton structure. For threads containing three copper filaments, C3C3A (0.0250 ± 0.0001 Ω/cm) and C3C3B (0.0273 ± 0.0001 Ω/cm) exhibit higher resistance than the uncoated C3C3n (0.0197 ± 0.0001 Ω/cm), indicating that coatings A and B increase resistance by approximately 27% and 39%, respectively, suggesting that partial coating discontinuity or increased contact resistance may outweigh conductive contributions at lower copper content. Structural configuration was also examined by comparing single-twisted and double-twisted architectures. P2C4n and P2C4n-DT, and C3C4n and C3C4n-DT, showed identical resistance values (0.0197 ± 0.0001 Ω/cm), demonstrating that double twisting does not significantly influence electrical performance within the present design. Overall, these comparisons indicate that copper filament content primarily governs electrical behavior, while coating effects are substrate-dependent and non-uniform, and structural variations such as double twisting exert negligible influence on resistance.
Electrical Conduction Mechanism of Twisted Copper–Carbon Textile Threads
The electrical behavior of the developed conductive threads can be explained by a multi-path conduction model consisting of metallic conduction through copper filaments and interfacial contact conduction between adjacent filaments. In the twisted structure, continuous copper filaments form the primary electron transport pathway, while additional current transfer occurs at filament-to-filament contact points. Therefore, the overall resistance of the thread is governed not only by the intrinsic resistivity of copper but also by the density and stability of electrical contact junctions created during twisting. Increasing the number of copper filaments enlarges the effective conductive cross-section and increases the number of parallel metallic pathways, which directly reduces total resistance. This explains the consistently lower resistance observed in threads containing higher copper filament content.
The carbon coating introduces a secondary conduction network that may either improve or deteriorate electrical performance depending on the structural configuration. When sufficient copper filaments are present, the carbon layer bridges microscopic gaps between adjacent fibers and stabilizes contact points, acting as a parallel resistor network that reduces contact resistance. This effect is particularly evident in cotton-based threads, where the porous and absorbent fiber structure allows deeper penetration of the coating and formation of conductive interconnections between filaments [28,29]. In contrast, when copper filament content is low, the coating partially covers metallic surfaces and introduces additional interface boundaries between copper and carbon particles. These interfaces increase junction resistance due to imperfect electrical contact and discontinuous conductive domains, leading to higher overall resistance despite the presence of a conductive coating [20].
The negligible influence of double twisting on resistance indicates that macroscopic yarn geometry does not significantly modify the internal conductive network once sufficient filament contact density has been established. Twisting primarily rearranges filament orientation but does not substantially change the number of electrical junctions per unit length; therefore, electron transport remains dominated by the intrinsic copper pathways. Overall, electrical conduction in the developed threads is controlled by a hybrid mechanism combining metallic conduction along copper filaments and contact resistance across filament junctions, with the coating acting either as a conductive bridge or an interfacial barrier, depending on filament density and fiber substrate characteristics.
3.3. Comparative Analysis of Conductive Threads Resistances with Commercial Conductive Threads
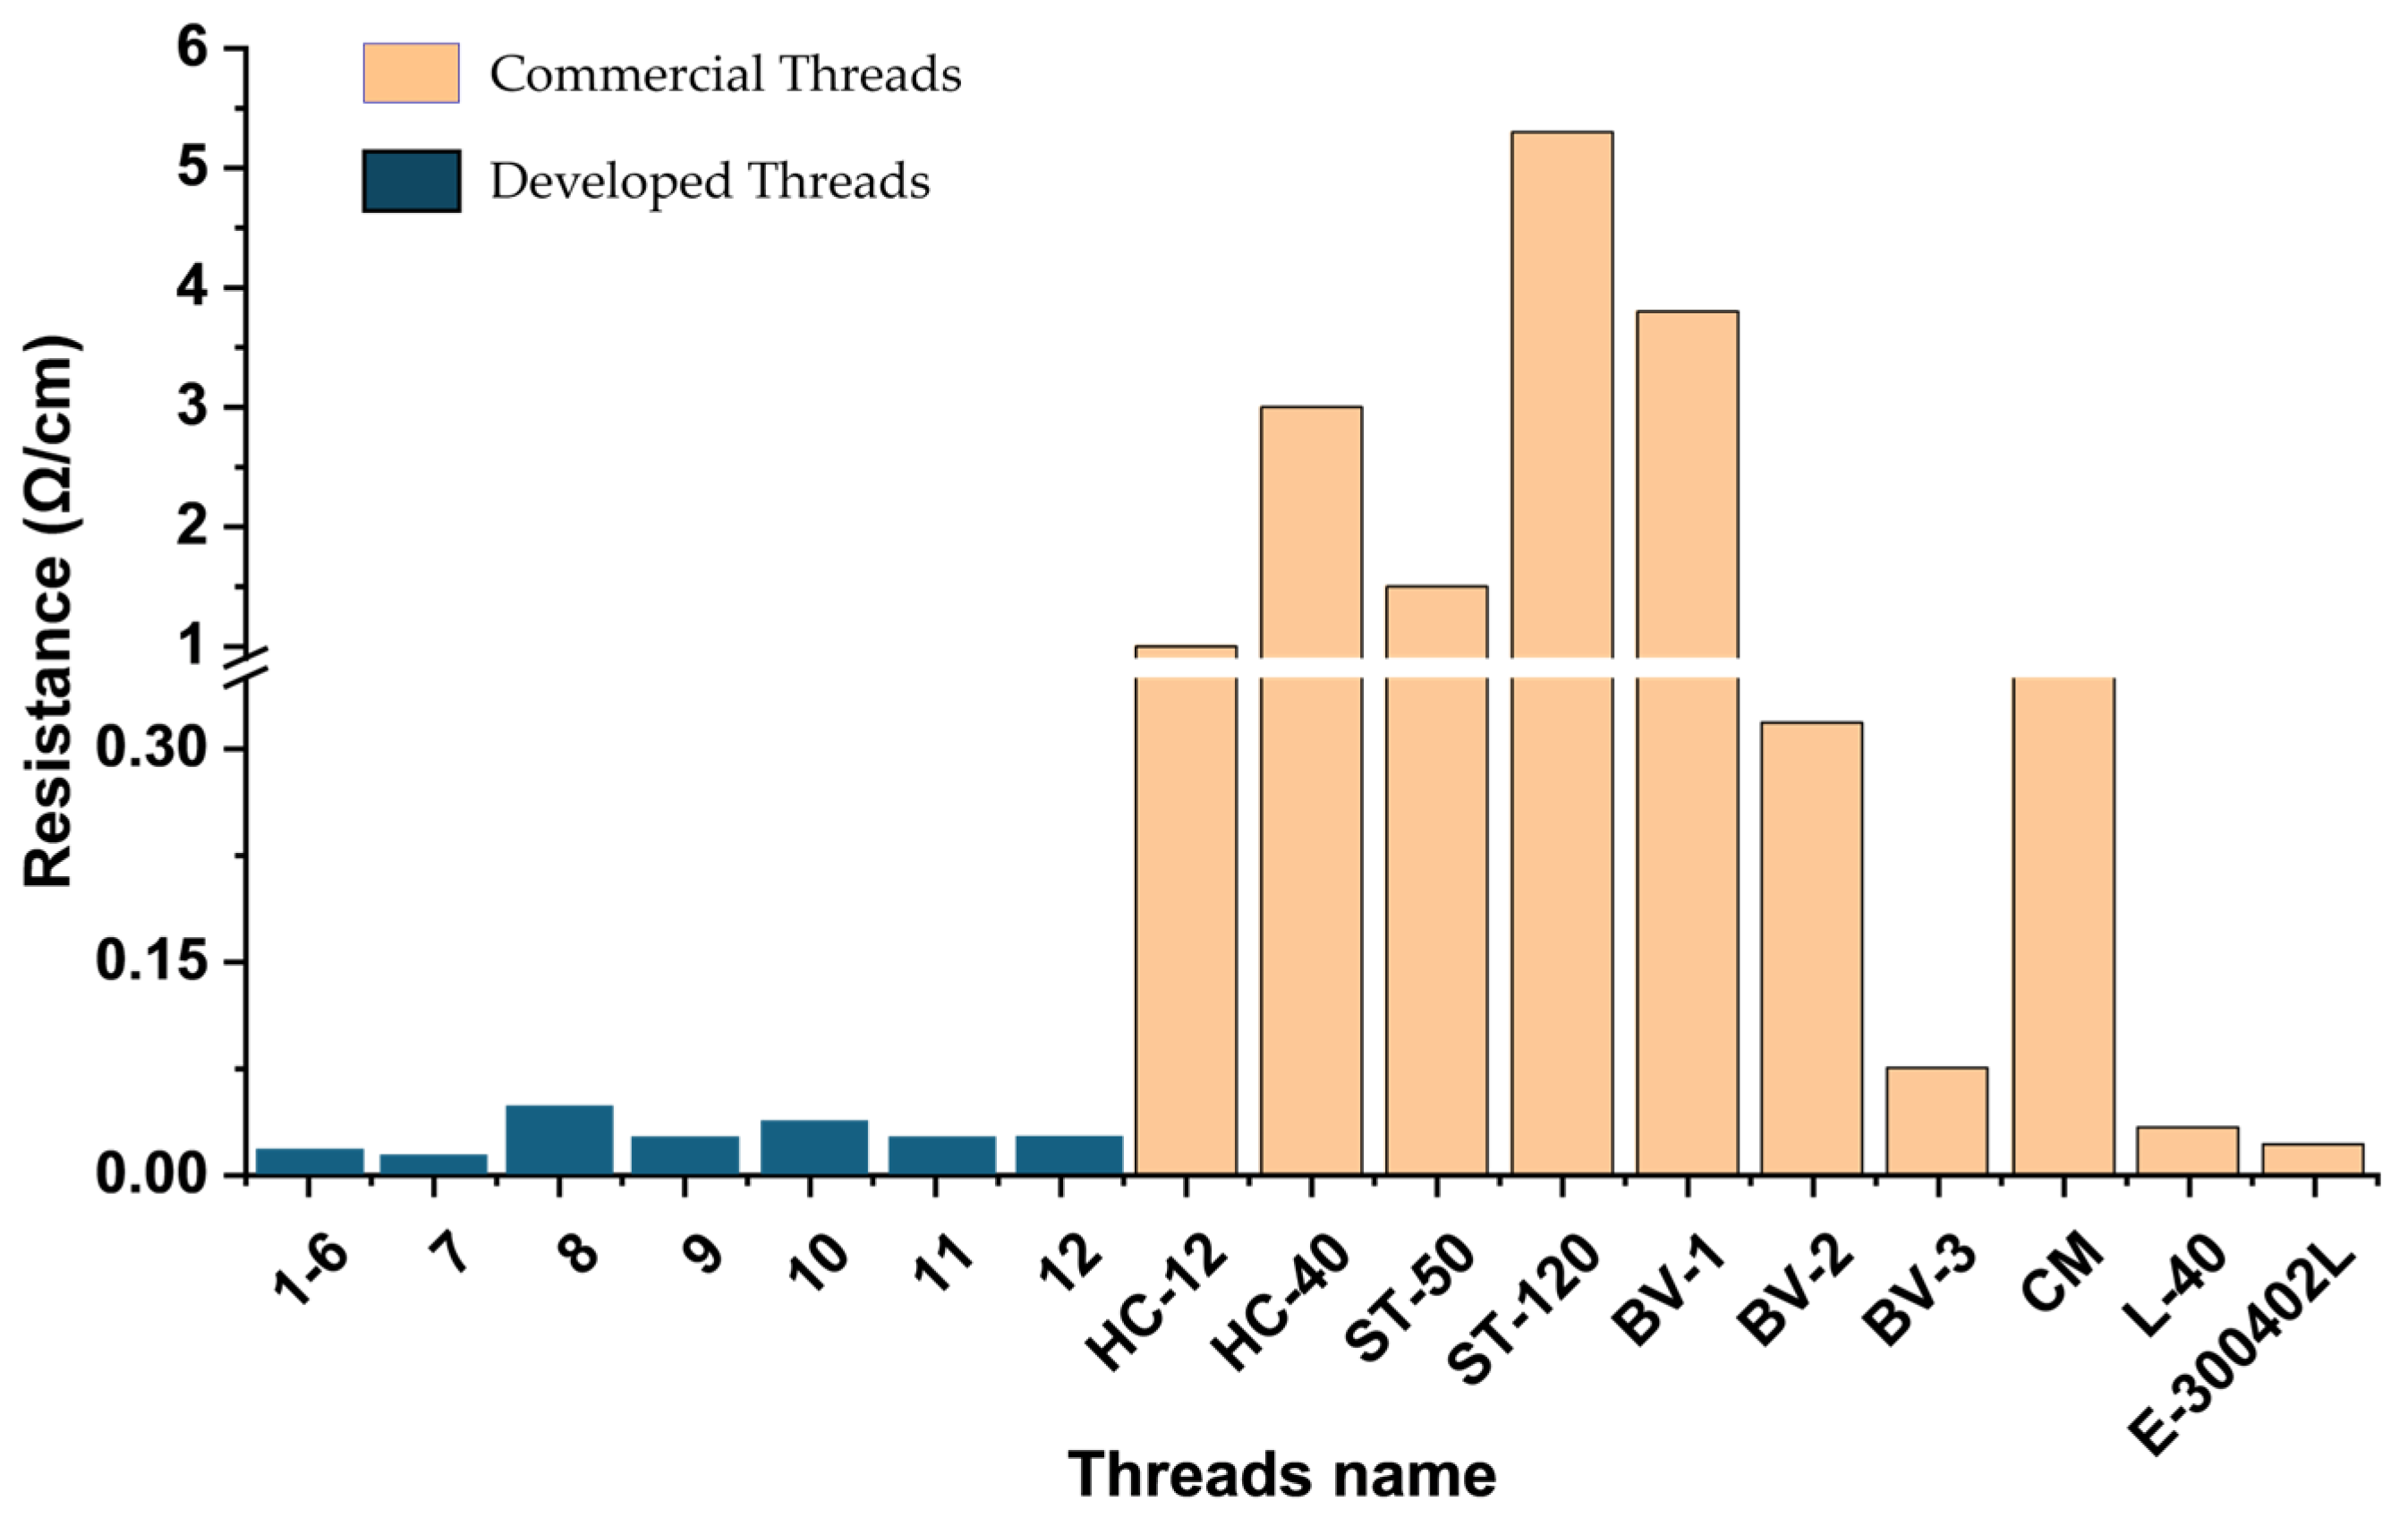
The electrical resistance of the developed conductive threads was compared with several commercially available conductive yarns reported in the literature and manufacturer data (Figure 5, Table S1). Silver-plated polyamide threads such as Madeira HC 40 (HC-40) and Madeira HC 12 (HC-12) (MADEIRA Garnfabrik) exhibit resistance values of approximately 3 Ω/cm and 1 Ω/cm, respectively [27]. Among stainless-steel-based commercial threads, Bekinox® VN type 140NY/35/2/140NY/350 (BV-1) shows a resistance of approximately 3.8 Ω/cm, while Bekinox® VN type 12/1x275/100z (BV-2), produced from continuous stainless-steel filaments, presents a lower resistance of 0.318 Ω/cm [30]. Moreover, VN12/4x275/100S/316L (BV-3) exhibits a resistance of 0.075 Ω/cm [31]. Silver Tech-50 (ST-50) and Silver Tech-120 (ST-120) display reported resistances of 1.5 Ω/cm and 5.3 Ω/cm, respectively [32], whereas Coats Magellan (CM), composed of 70% steel and 30% polyester, exhibits an internal resistance of approximately 0.6 Ω/cm [33]. More recent commercial conductive yarns, such as Liberator 40 and Elektrisola 3000402L, report resistance values of approximately 0.030 Ω/cm and 0.021 Ω/cm, respectively.
Figure 5.
Comparison of developed conductive threads with commercially available conductive threads. Error bars are included but may be smaller than the symbol size.
In comparison, the developed twisted copper-based threads exhibited resistance values ranging from 0.0164 ± 0.0001 Ω/cm to 0.0470 ± 0.0001 Ω/cm. Threads 1–6 showed consistent resistance of approximately 0.0197 ± 0.0001 Ω/cm, while Thread 7 (C3C4A) demonstrated the lowest resistance of 0.0164 ± 0.0001 Ω/cm. Compared with state-of-the-art commercial lower resistance yarns such as Liberator 40 and Elektrisola 3000402L [34,35], Thread 7 exhibits comparable or moderately lower resistance (approximately 1.3–2.0× improvement). Even the finest developed thread (Thread 10, 4.5 Ne), with a resistance of 0.0459 ± 0.0001 Ω/cm, remains competitive with most silver-plated and stainless steel-based commercial yarns.
These results indicate that the developed threads achieve electrical performance comparable to or slightly exceeding that of modern commercial conductive yarns. This performance is primarily attributed to the presence of continuous copper filaments within the twisted structure, which provide efficient conductive pathways compared to stainless-steel or silver-coated polymer yarns. The findings demonstrate that the proposed threads offer competitive low-resistance characteristics suitable for applications requiring minimal resistive loss, including wearable electronic systems.
3.4. Resistance Dynamics of Conductive Threads Under Wash–Dry Cycles
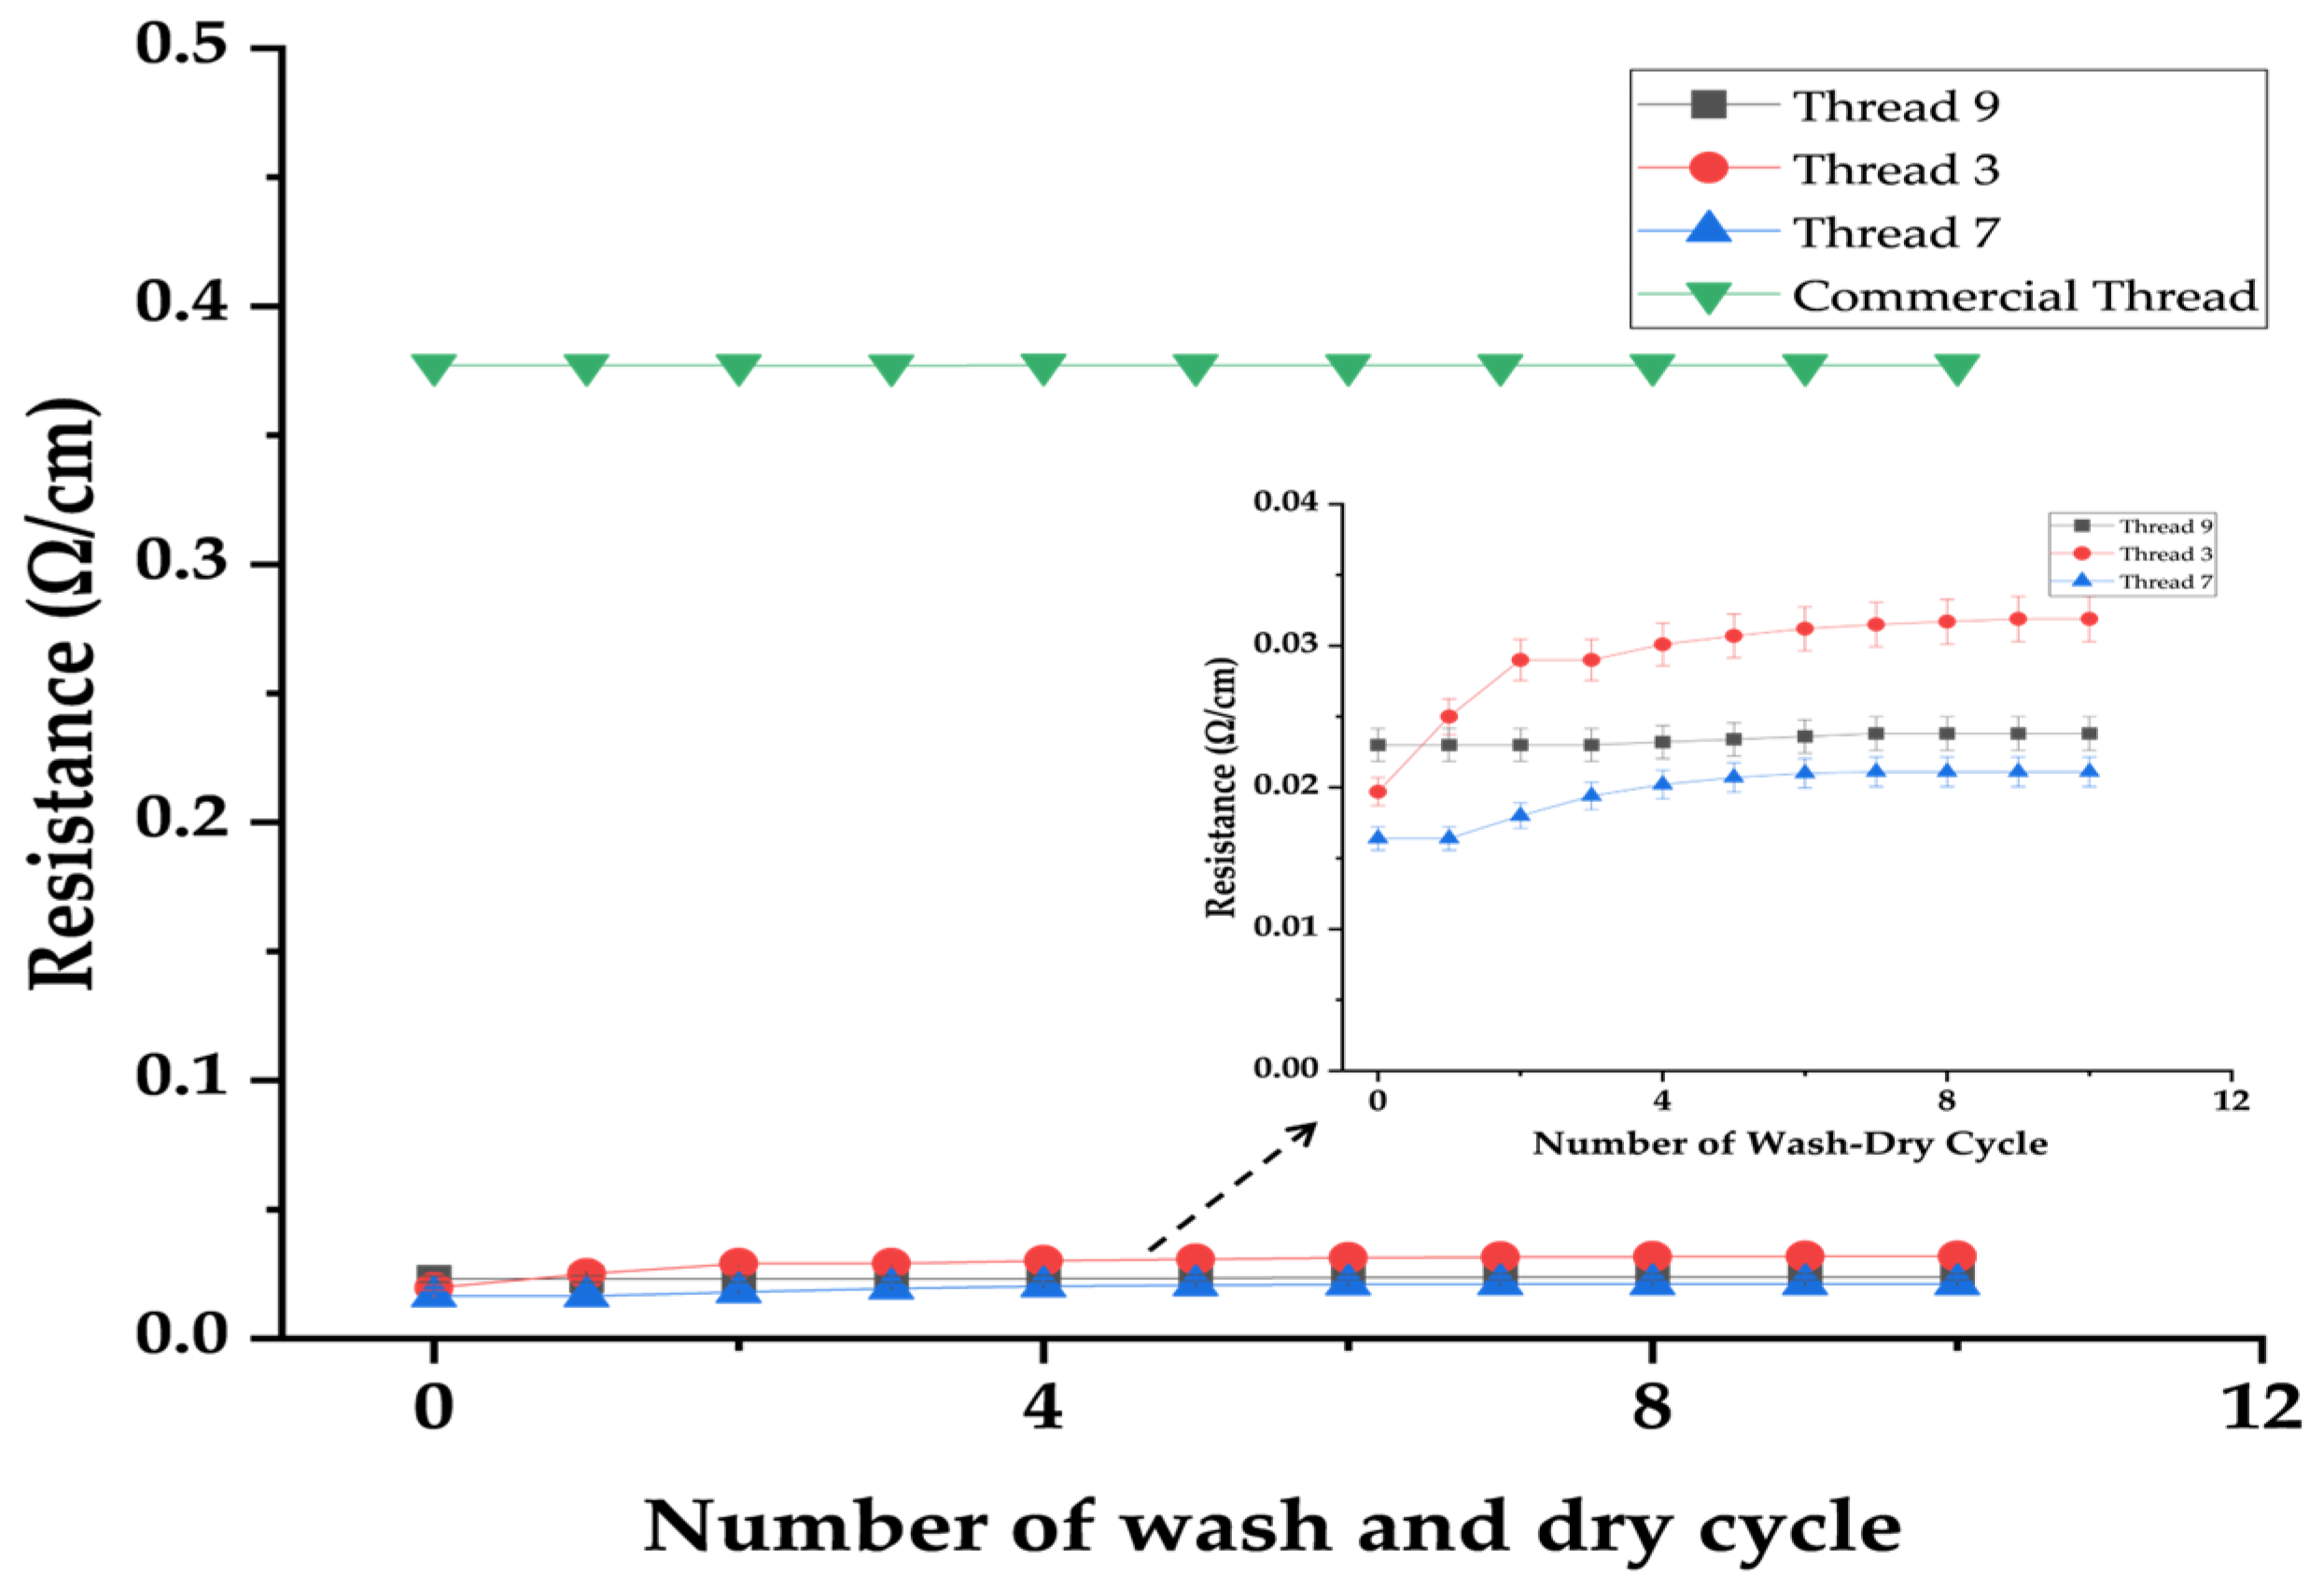
Figure 6 shows the resistance variation during the wash–dry cycles. Thread No. 9 (P2C3n) exhibited minimal resistance change over ten cycles. The resistance remained stable at 0.0230 Ω/cm during the first three cycles and slightly increased to 0.0238 Ω/cm thereafter, with no significant fluctuation from cycle 7 to 10. This minor increase may be attributed to slight structural relaxation within the twisted filament bundle, leading to marginal changes in filament contact. Thread No. 3 (P2C4A) initially exhibited a resistance of 0.0197 Ω/cm but showed a gradual increase across cycles, reaching 0.0319 Ω/cm after ten cycles. This trend suggests partial degradation or detachment of the carbon coating under repeated washing stress. In contrast, Thread No. 7 (C3C4A) demonstrated improved stability. Although its resistance increased slightly from 0.0164 Ω/cm to 0.0210 Ω/cm, the variation remained moderate and stabilized after cycle 7. Statistical analysis using a paired t-test indicated that the resistance changes observed for Threads 9 and 7 across wash–dry cycles were not statistically significant (p > 0.05), confirming stable electrical performance under laundering conditions. The comparatively better performance of the cotton-based coated thread may be associated with the hydrophilic and porous nature of cotton fibers, which can enhance coating adhesion relative to polyester substrates [28,29]. For comparison, the commercial stainless steel conductive thread Bekinox® VN (12/1x275/100z) exhibited negligible resistance variation throughout the wash cycles, consistent with the mechanical robustness and intrinsic conductivity of stainless-steel multifilament yarns [36]. The observed resistance increase in some samples can be interpreted using the fundamental resistance relation:
where R is resistance, is resistivity, L is length, and A is cross-sectional area. Mechanical agitation and repeated drying may cause partial loss of the carbon coating and structural rearrangement of the twisted filament bundle. These effects do not change the physical diameter of the copper filaments; however, they can reduce the effective electrical contact area between adjacent filaments and increase inter-filament contact resistance. As a result, the continuity of conductive pathways becomes less efficient, leading to an increase in the measured resistance. Minor resistance fluctuations observed during wash–dry cycling are comparable to the instrument repeatability (±0.001–0.002 Ω/cm) and may partly originate from measurement uncertainty. However, the consistent trends across multiple cycles indicate that larger resistance changes in the coated samples arise primarily from coating degradation and filament rearrangement rather than experimental error. The result of wash–dry cycles indicates that uncoated twisted copper threads demonstrated superior wash durability compared to carbon-coated variants, as evidenced by their lower resistance variation over ten cycles. While both thread categories maintained functional conductivity, the findings suggest that uncoated twisted copper threads are more suitable for washable smart textile applications, whereas carbon-coated threads may be preferable for applications with limited laundering exposure.
Figure 6.
Stability tests under washing and drying cycles in water showing the electrical resistance of the conductive threads. Error bars are included but may be smaller than the symbol size.
3.5. Mechanical–Electrical Stability of Conductive Threads Under Bending and Twisting
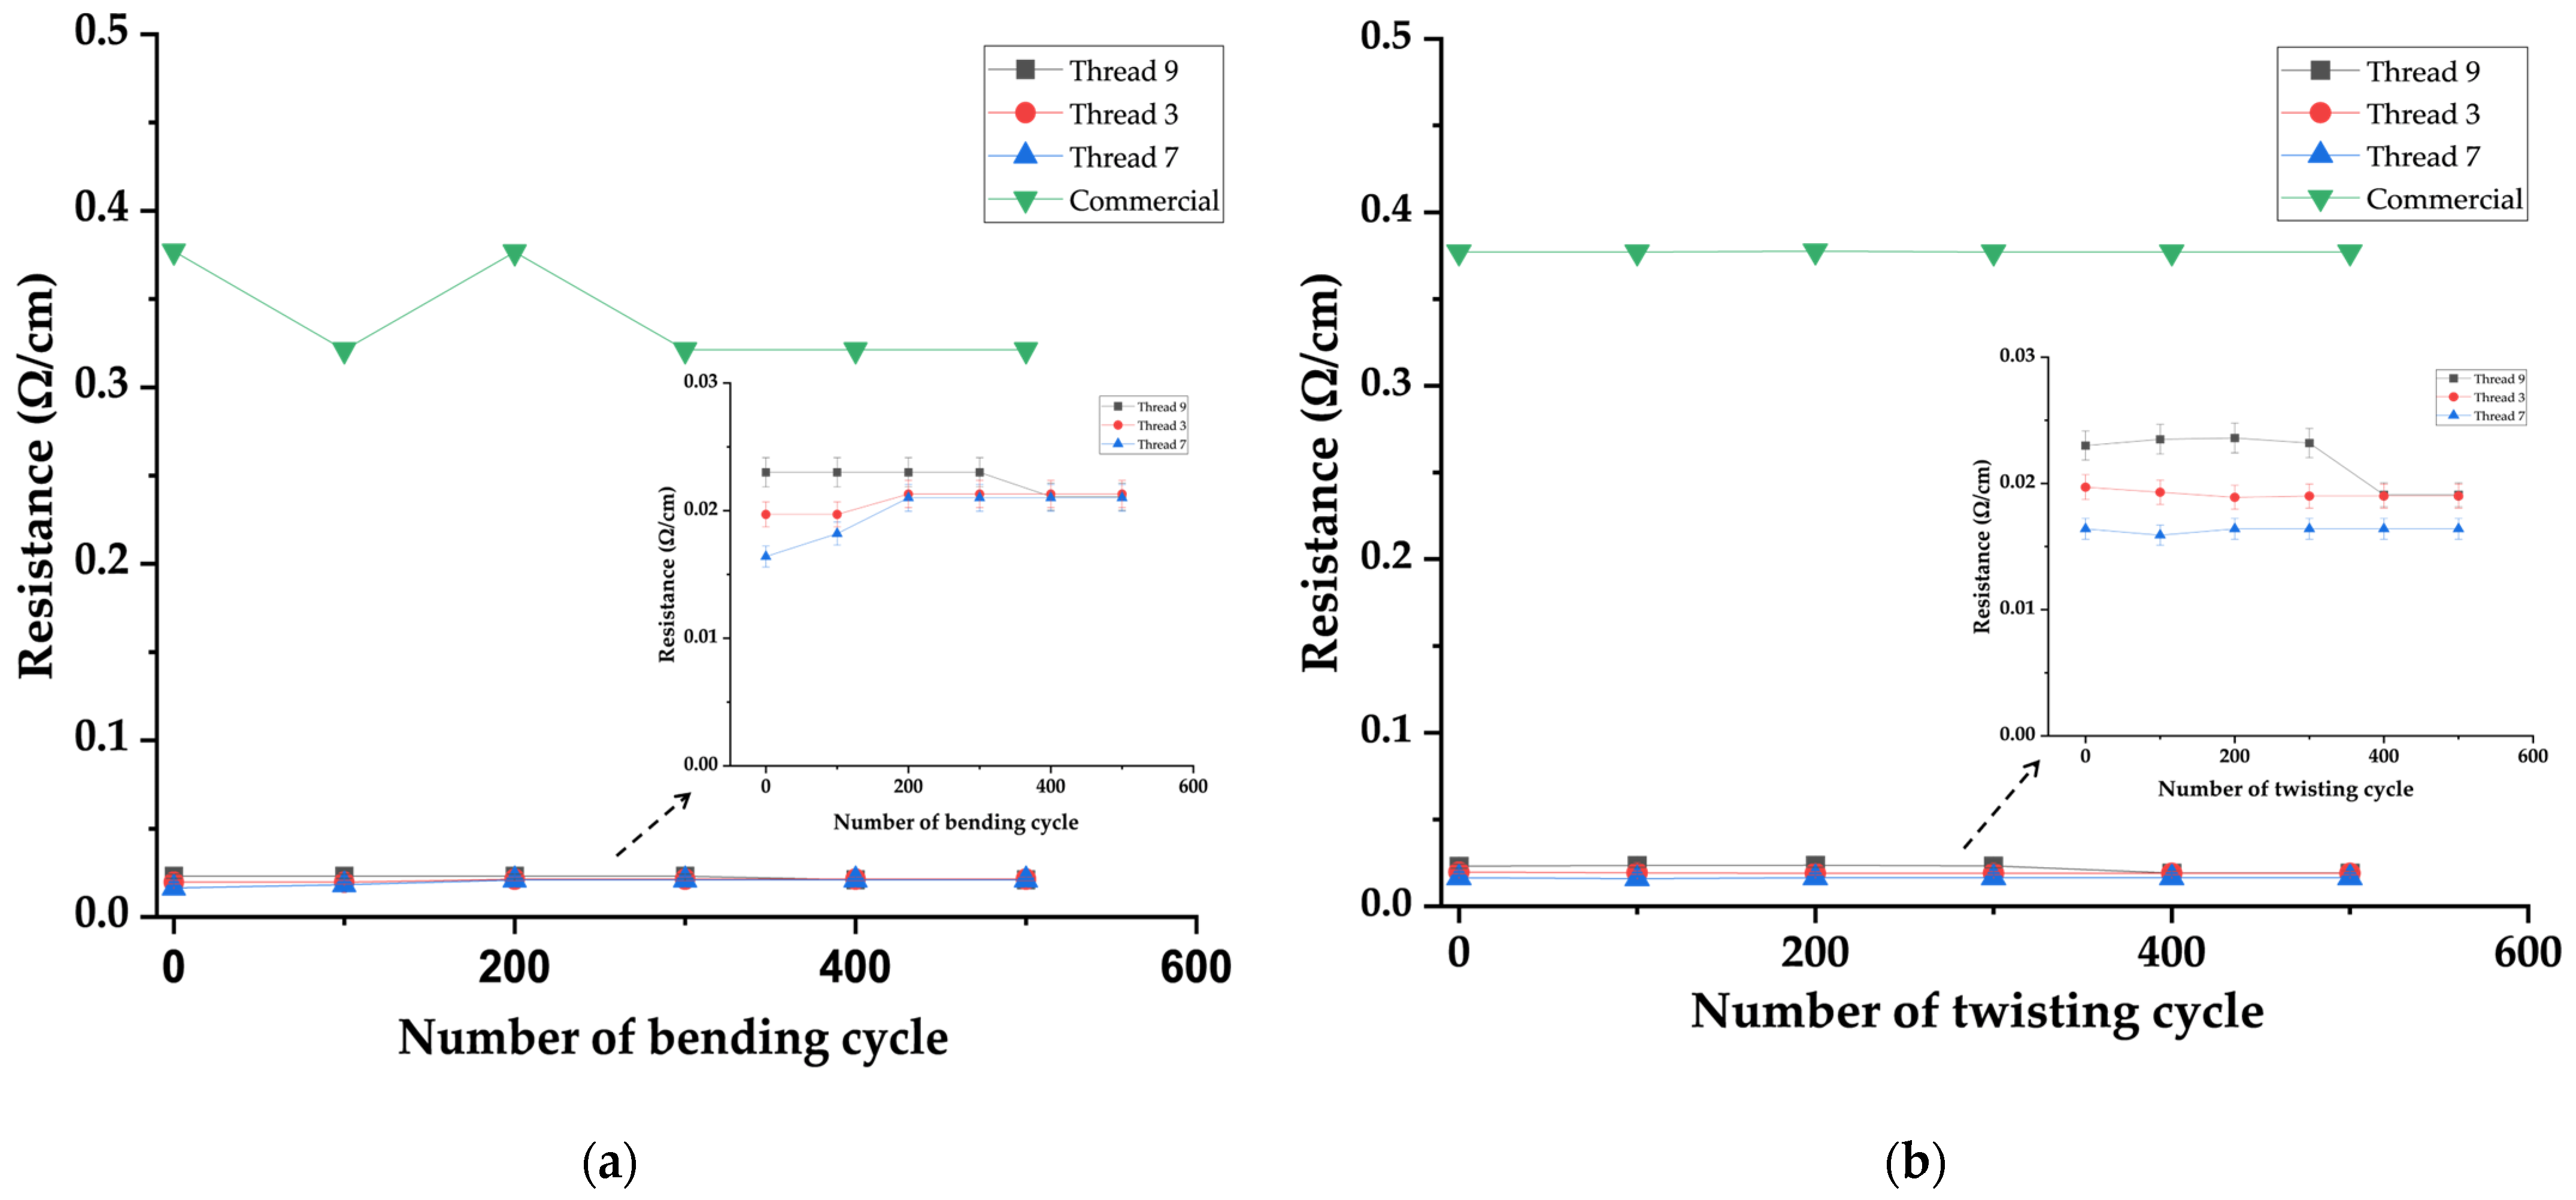
The mechanical durability and electrical stability of Thread 9, Thread 3, and Thread 7 were evaluated under 500 cycles of repeated bending (150°) and twisting (360°). The resistance variation during cyclic deformation is presented in Figure 7. The performance was compared with the commercial stainless steel conductive thread Bekinox® VN (12/1x275/100z).
Figure 7.
Mechanical–electrical stability of conductive threads under repeated (a) bending, and (b) twisting deformation. Error bars are included but may be smaller than the symbol size.
During cyclic bending (Figure 7a), all the developed threads exhibited minimal resistance variation, indicating good flexibility and mechanical integrity. Thread 9 remained stable at 0.0230 Ω/cm up to 300 cycles and slightly decreased to 0.0211 Ω/cm after 500 cycles. Thread 3 showed a modest increase from 0.0197 to 0.0213 Ω/cm, while Thread 7 increased from 0.0164 to 0.0210 Ω/cm by cycle 200 and then stabilized for the remaining cycles. The slight resistance increases observed in some samples may be attributed to minor structural relaxation within the twisted filament bundle, leading to small variations in filament contact. The minor resistance reductions observed in certain cases can be associated with internal compaction during bending, which may improve filament-to-filament contact and enhance electrical pathways. Conversely, the commercial Bekinox® VN thread exhibited resistance variation from 0.3770 Ω/cm to 0.3212 Ω/cm after 500 cycles. Although it maintained relatively stable behavior, its absolute resistance remained substantially higher than that of the developed copper-based threads.
Under repeated twisting (Figure 7b), all the developed threads demonstrated highly stable resistance over 500 cycles. Thread 9 decreased slightly from 0.0230 to 0.0191 Ω/cm. Thread 3 remained nearly constant, varying between 0.0197 and 0.0190 Ω/cm. Thread 7 showed the highest stability, with negligible change from its initial resistance of 0.0164 Ω/cm. The small decreases observed in Threads 3 and 9 may be attributed to improved alignment and tighter contact among copper filaments under torsional stress, which can enhance conductive pathways. The commercial Bekinox® VN thread also showed negligible variation during twisting. These results indicate that the developed twisted copper conductive threads maintain comparatively stable electrical performance under repeated mechanical deformation. The combination of low absolute resistance and minimal variation under bending and twisting demonstrates strong mechanical–electrical stability suitable for flexible and wearable electronic applications. Statistical analysis using a paired t-test confirmed that the resistance changes observed in Threads 9, 3, and 7 after 500 bending and twisting cycles were not statistically significant (p > 0.05), further supporting the stability of the developed conductive threads under repeated mechanical deformation.
3.6. Overall Performance Evaluation
Considering the combined results of morphological analysis, electrical resistance measurement, wash–dry durability, and cyclic mechanical deformation, Thread 7 (C3C4A) demonstrated the most balanced performance among the developed samples. Thread 7 exhibited the lowest initial resistance of 0.0164 ± 0.0001 Ω/cm and maintained stable electrical behavior under bending and twisting over 500 cycles. Although a moderate resistance increase was observed during wash–dry testing, the absolute resistance remained significantly lower than that of the commercial stainless-steel thread after each cycle. The minor variation observed after laundering is not expected to compromise functional performance, as the twisted copper filament core ensures continuous conductive pathways even if partial coating degradation occurs. From a materials perspective, the incorporation of ultra-fine copper filaments combined with carbon paste coating provides an effective balance between conductivity and mechanical flexibility. In addition, the use of recycled e-waste-derived carbon materials supports sustainable material utilization and cost reduction relative to conventional conductive coatings. Compared with reported resistance values of silver nanowire-coated textile threads [16], graphene-based conductive cotton threads [5], and SWCNT or PEDOT: PSS-coated yarns [17], the developed copper-based threads exhibit competitive or lower resistance values under similar measurement units. However, differences in fabrication methods, coating thickness, and testing conditions should be considered when making direct comparisons. Taken together, the results indicate that Thread 7 offers a strong combination of low resistance, mechanical durability, and wash stability, making it a promising candidate for wearable and smart textile applications.
3.7. Conductive Threads: Future Textiles
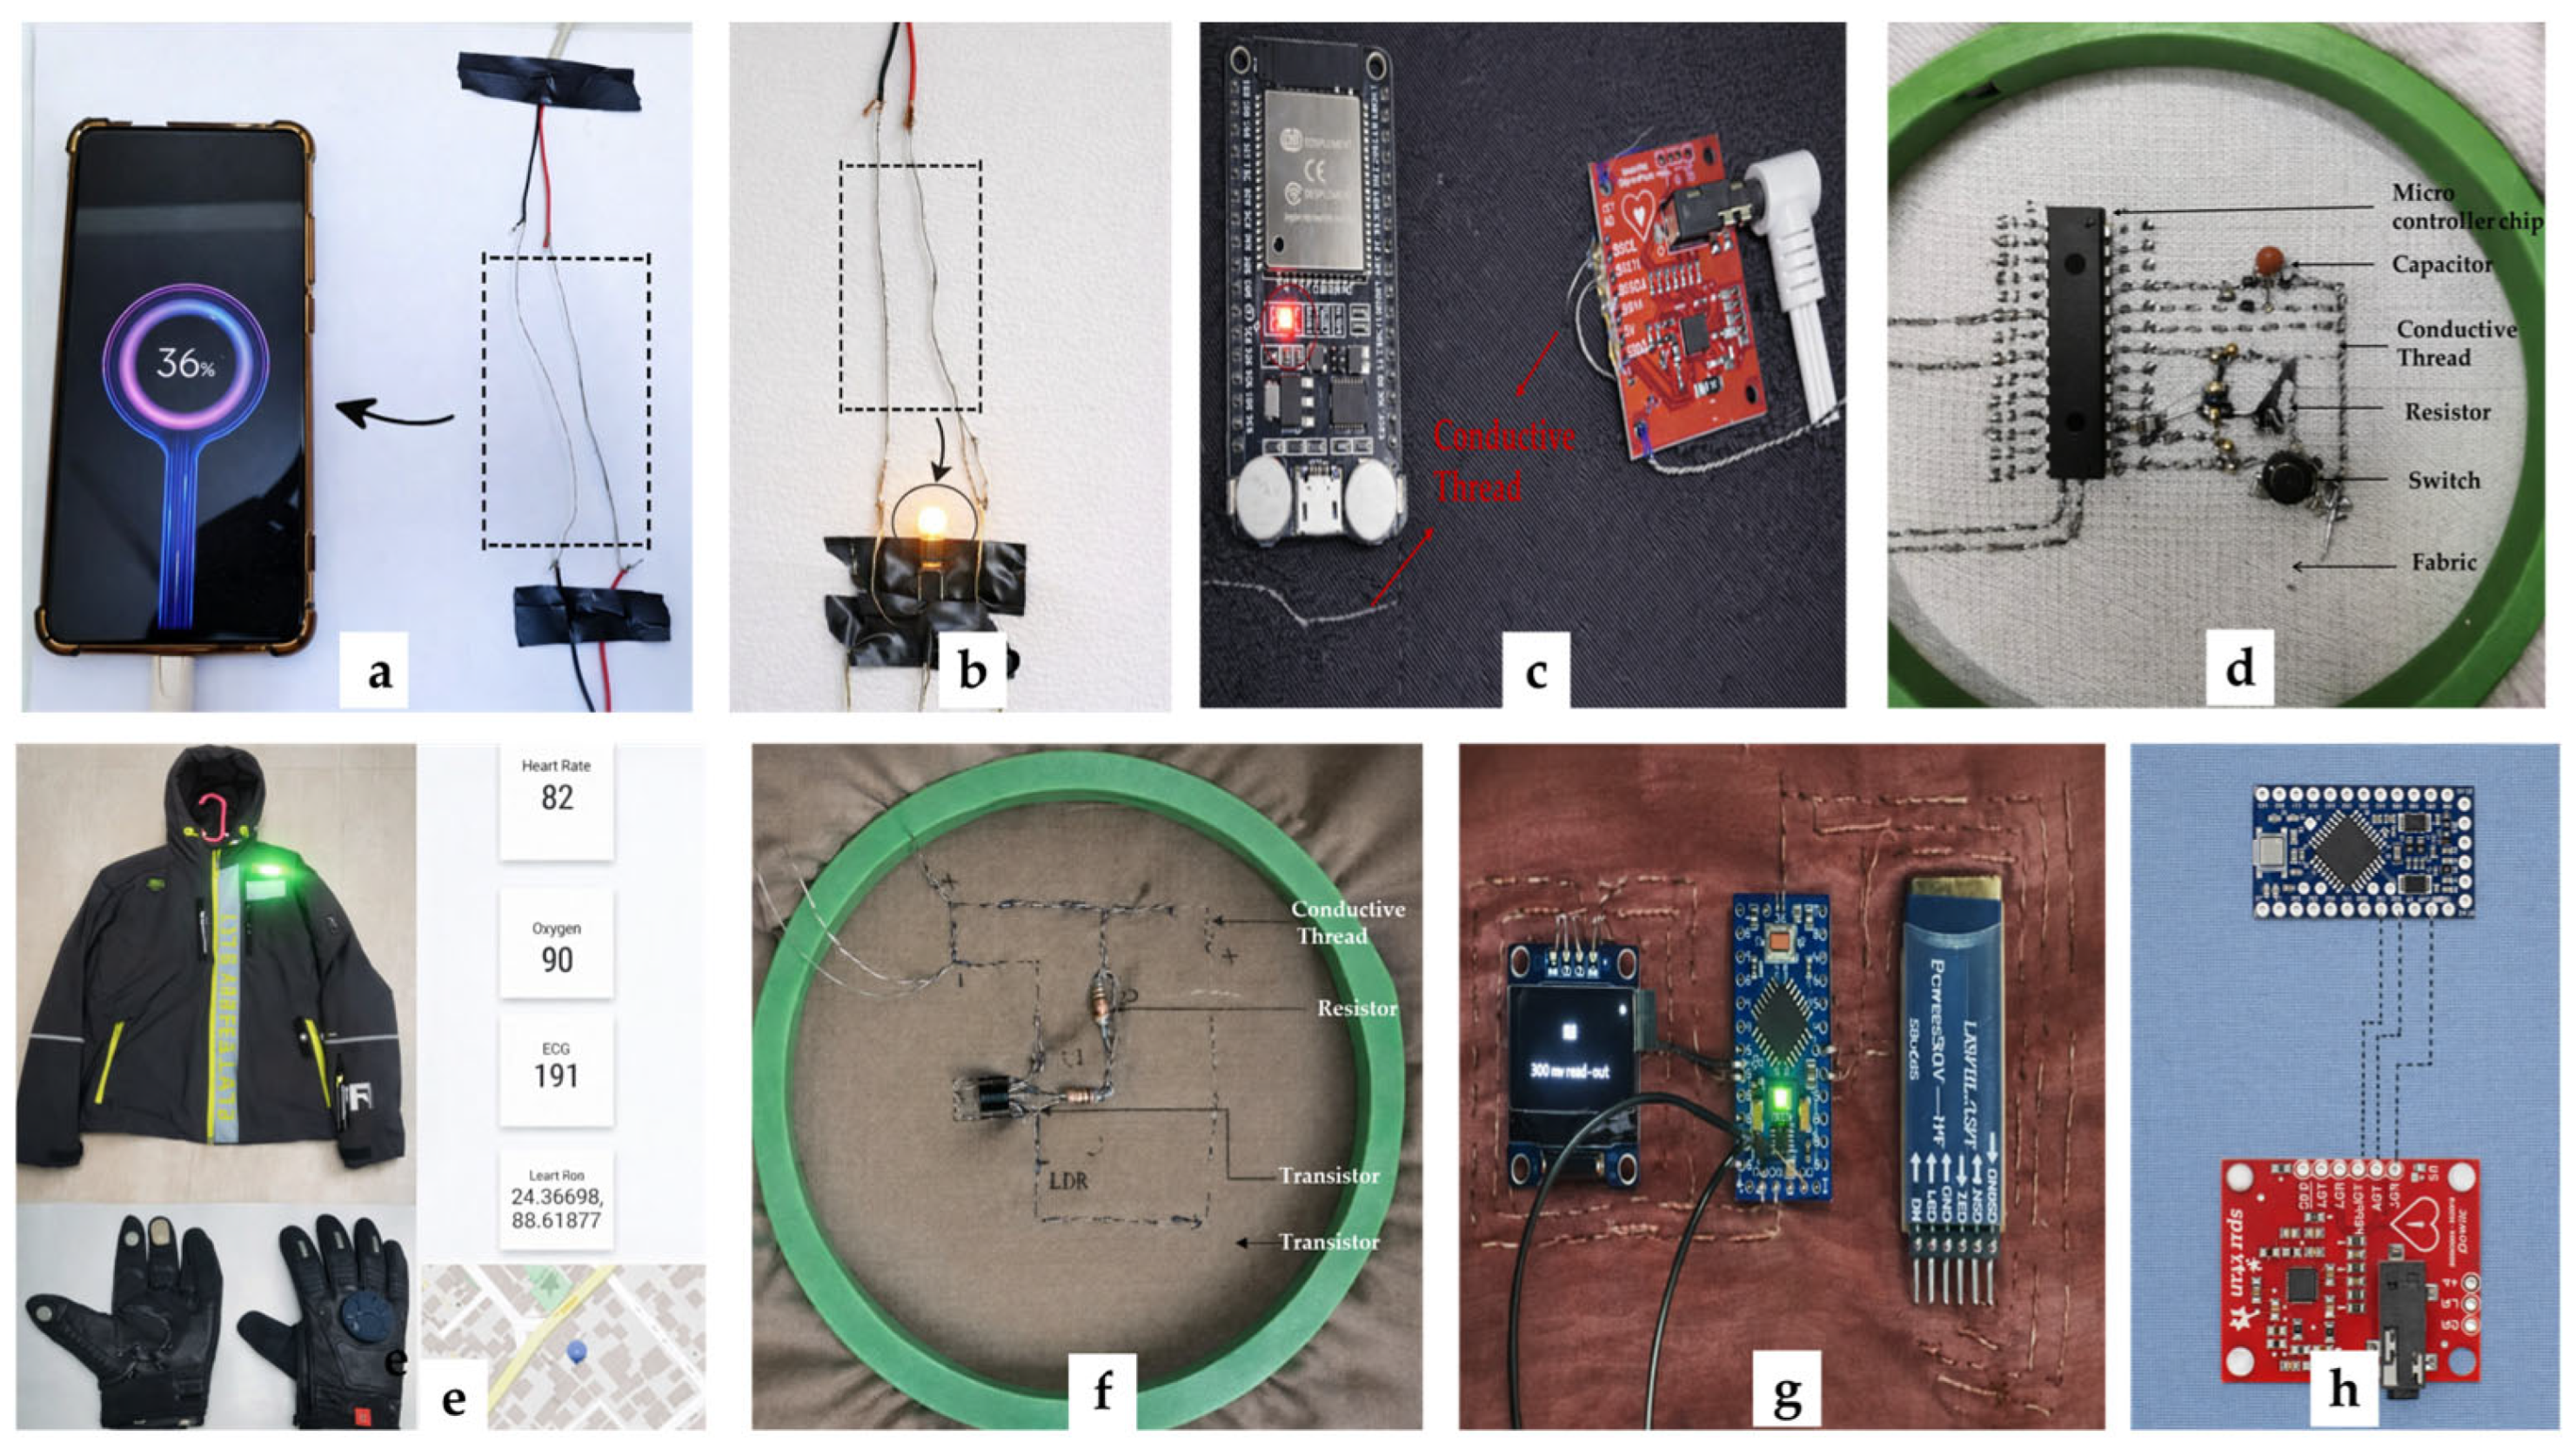
Wearable electronic textiles integrated into smart garments are increasingly explored for applications in healthcare monitoring, sports performance tracking, occupational safety, rehabilitation, and interactive systems [37]. In this study, the developed conductive threads were evaluated in practical textile-based electronic configurations to assess their functional applicability. The conductive threads were used to replace conventional copper wires in a smartphone charging circuit, as shown in Figure 8a. The charging operation remained stable, demonstrating that the threads can sustain low-voltage power transmission with minimal resistive loss. Similarly, the threads were used in place of standard connecting wires in light-emitting diode circuits (Figure 8b), where consistent illumination confirmed reliable current conduction. To further demonstrate integration capability, the conductive threads were embedded into fabric to form textile-based electrical interconnections. These interconnections supported an AD8232 ECG sensor integrated with an ESP32 and Arduino Uno-based system (Figure 8c,d), which was incorporated into a smart jacket (Figure 8e). The stable operation of the sensor module indicates that the threads can support low-power signal transmission and data acquisition within wearable systems. In addition, flexible fabric circuits and textile-based printed circuit boards were fabricated using the developed conductive threads (Figure 8f–h). The threads maintained structural flexibility while enabling electrical connectivity between components, demonstrating their suitability for deformable electronic platforms [38]. The combination of low electrical resistance, mechanical flexibility, wash durability, and compatibility with textile integration suggests that these conductive threads are viable candidates for smart textile systems. Their fabrication approach, including the use of recycled carbon materials, also supports sustainable and cost-effective development of wearable electronic technologies.
Figure 8.
Practical demonstrations of the developed conductive threads for wearable textile applications: (a) smartphone charging using conductive threads as power transmission lines; (b) LED illumination test confirming current conduction; (c) integration of ESP32 and AD8232 ECG sensor through textile interconnections [37]; (d) connection of Arduino-compatible modules using conductive threads; (e) smart jacket prototype demonstrating real-time physiological monitoring [37]; (f) fabric circuit integrating LDR and transistor elements; (g) functional embedded system with display and Bluetooth module assembled on fabric; and (h) microcontroller-based textile circuit incorporating passive components.
4. Conclusions
This study demonstrates the development and systematic evaluation of twelve conductive thread variants designed for smart textile applications. The electrical, mechanical, and laundering analyses confirm that twisted copper-based conductive threads can achieve low resistance while maintaining flexibility and structural stability under practical use conditions. Among the developed samples, Thread 7 (C3C4A) exhibited the most balanced performance, with the lowest measured resistance of 0.0164 ± 0.0001 Ω/cm and stable behavior under bending, twisting, and wash–dry cycles. The results indicate that the combination of ultra-fine copper filaments and carbon coating on a cotton substrate provides effective conductive pathways while preserving mechanical integrity. Although moderate resistance variation was observed during repeated laundering, functional conductivity was retained across all the developed threads. Comparative analysis with commercially available conductive yarns shows that the developed threads achieve significantly lower resistance values while maintaining flexibility and wash durability. The successful demonstration of smartphone charging, LED operation, textile-based circuits, embedded sensor systems, and a smart jacket prototype confirms the feasibility of integrating these conductive threads into wearable electronic platforms. The use of carbon paste derived from electronic waste supports a sustainable material approach and offers a cost-conscious alternative to conventional conductive coatings. This strategy contributes to environmentally responsible material development while maintaining competitive electrical performance. Future work should focus on scalable fabrication methods, improved coating fixation strategies to enhance laundering stability, long-term durability evaluation, and expanded application testing. The fabrication approach may also be adapted to other natural cellulosic fibers, supporting broader adoption of renewable materials in smart textile systems. The findings of this research establish twisted copper-based conductive threads as promising candidates for wearable electronics, smart garments, and flexible textile-integrated electronic systems.
Supplementary Materials
The following supporting information can be downloaded at: https://www.mdpi.com/article/10.3390/fib14030036/s1, Table S1: Electrical resistance comparison of developed conductive threads (DT) with commercial benchmark threads.
Author Contributions
A.U.A.K.: Conceptualization, investigation, methodology, formal analysis, and writing—original draft. N.N.: Conceptualization, investigation, methodology, formal analysis, and writing—original draft. M.H.R.: Conceptualization and methodology. A.K.S.: Resources. Z.T.B.: Data Analysis. A.B.: Supervision and writing—review and editing. A.M.M.: Writing—Review and Editing. All authors have read and agreed to the published version of the manuscript.
Funding
This research received no external funding.
Data Availability Statement
All data analyzed during this study are included in this published article and its Supplementary Materials. The datasets are fully represented in the graphs and tables provided, and no additional data is available.
Acknowledgments
During the preparation of this manuscript, the authors used Gemini Pro and ChatGPT 5.2 for grammatical checking. The authors have reviewed and edited the output and take full responsibility for the content of this publication.
Conflicts of Interest
The authors declare no conflicts of interest.
References
- Dong, H.; Wang, D.; Sun, G.; Hinestroza, J.P. Assembly of metal nanoparticles on electrospun nylon 6 nanofibers by control of interfacial hydrogen-bonding interactions. Chem. Mater. 2008, 20, 6627–6632. [Google Scholar] [CrossRef] [Scilit]
- Shuai, L.; Guo, Z.H.; Zhang, P.; Wan, J.; Pu, X.; Wang, Z.L. Stretchable, self-healing, conductive hydrogel fibers for strain sensing and triboelectric energy-harvesting smart textiles. Nano Energy 2020, 78, 105389. [Google Scholar] [CrossRef] [Scilit]
- Cherenack, K.; Van Pieterson, L. Smart textiles: Challenges and opportunities. J. Appl. Phys. 2012, 112, 91301. [Google Scholar] [CrossRef] [Scilit]
- Tang, Y.; Guo, B.; Cruz, M.A.; Chen, H.; Zhou, Q.; Lin, Z.; Xu, F.; Xu, F.; Chen, X.; Cai, D. Colorful conductive threads for wearable electronics: Transparent Cu–Ag nanonets. Adv. Sci. 2022, 9, 2201111. [Google Scholar] [CrossRef] [Scilit]
- Alhashmi Alamer, F.; Almalki, G.A.; Althagafy, K. Advancements in Conductive Cotton Thread-Based Graphene: A New Generation of Flexible, Lightweight, and Cost-Effective Electronic Applications. J. Compos. Sci. 2023, 7, 476. [Google Scholar] [CrossRef] [Scilit]
- Lam Po Tang, S.; Stylios, G. An overview of smart technologies for clothing design and engineering. Int. J. Cloth. Sci. Technol. 2006, 18, 108–128. [Google Scholar] [CrossRef] [Scilit]
- Tsukada, S.; Nakashima, H.; Torimitsu, K. Conductive polymer combined silk fiber bundle for bioelectrical signal recording. PLoS ONE 2012, 7, e33689. [Google Scholar] [CrossRef] [Scilit]
- Cheng, H.; Dong, Z.; Hu, C.; Zhao, Y.; Hu, Y.; Qu, L.; Chen, N.; Dai, L. Textile electrodes woven by carbon nanotube–graphene hybrid fibers for flexible electrochemical capacitors. Nanoscale 2013, 5, 3428–3434. [Google Scholar] [CrossRef] [Scilit]
- Ajani, A.; Gilani, H.; Islam, S.; Khandoker, N.; Mazid, A.M. Fabrication of CNT-reinforced 6061 aluminium alloy surface composites by friction stir processing. JOM 2021, 73, 3718–3726. [Google Scholar] [CrossRef] [Scilit]
- Jung, S.; Lee, J.; Hyeon, T.; Lee, M.; Kim, D.-H. Fabric-based integrated energy devices for wearable activity monitors. Adv. Mater. 2014, 26, 6329–6334. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Liu, H.; Goh, W.-P.; Norsten, T.B. Aqueous-based formation of gold nanoparticles on surface-modified cotton textiles. J. Mol. Eng. Mater. 2013, 1, 1250001. [Google Scholar] [CrossRef] [Scilit]
- Dong, B.H.; Hinestroza, J.P. Metal nanoparticles on natural cellulose fibers: Electrostatic assembly and in situ synthesis. ACS Appl. Mater. Interfaces 2009, 1, 797–803. [Google Scholar] [CrossRef] [Scilit]
- Lee, J.; Kwon, H.; Seo, J.; Shin, S.; Koo, J.H.; Pang, C.; Son, S.; Kim, J.H.; Jang, Y.H.; Kim, D.E. Conductive fiber-based ultrasensitive textile pressure sensor for wearable electronics. Adv. Mater. 2015, 27, 2433–2439. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Guo, J.; Wang, Y.; Zhang, H.; Zhao, Y. Conductive materials with elaborate micro/nanostructures for bioelectronics. Adv. Mater. 2022, 34, 2110024. [Google Scholar] [CrossRef] [Scilit]
- Dev, B.; Alam, M.R.; Rahman, M.A.; Newaz, K.; Khan, M.A.; Rahman, M.Z. Advanced nanocomposites for sensing applications. In Comprehensive Materials Processing; Elsevier: Amsterdam, The Netherlands, 2023. [Google Scholar]
- Atwa, Y.; Maheshwari, N.; Goldthorpe, I.A. Silver nanowire coated threads for electrically conductive textiles. J. Mater. Chem. C 2015, 3, 3908–3912. [Google Scholar] [CrossRef] [Scilit]
- Alhashmi Alamer, F.; Badawi, N.M. Fully Flexible, Highly Conductive Threads Based on single walled carbon nanotube (SWCNTs) and poly (3, 4 ethylenedioxy thiophene) poly (styrenesulfonate) (PEDOT: PSS). Adv. Eng. Mater. 2021, 23, 2100448. [Google Scholar] [CrossRef] [Scilit]
- Wang, B.; Facchetti, A. Mechanically flexible conductors for stretchable and wearable e-skin and e-textile devices. Adv. Mater. 2019, 31, 1901408. [Google Scholar] [CrossRef] [Scilit]
- Islam, M.R.; Afroj, S.; Yin, J.; Novoselov, K.S.; Chen, J.; Karim, N. Advances in printed electronic textiles. Adv. Sci. 2024, 11, 2304140. [Google Scholar] [CrossRef] [Scilit]
- Cork, C. Conductive fibres for electronic textiles: An overview. In Electronic Textiles; Woodhead Publishing: Cambridge, UK, 2015; pp. 3–20. [Google Scholar]
- Dev, B.; Rahman, M.A.; Tazrin, T.; Islam, M.S.; Datta, A.; Rahman, M.Z. Investigation of Mechanical Properties of Nonwoven Recycled Cotton/PET Fiber-Reinforced Polyester Hybrid Composites. Macromol. Mater. Eng. 2024, 309, 2400020. [Google Scholar] [CrossRef] [Scilit]
- Grant, K.; Goldizen, F.C.; Sly, P.D.; Brune, M.-N.; Neira, M.; van den Berg, M.; Norman, R.E. Health consequences of exposure to e-waste: A systematic review. Lancet Glob. Health 2013, 1, e350–e361. [Google Scholar] [CrossRef] [Scilit]
- Vishwakarma, S.; Kumar, V.; Arya, S.; Tembhare, M.; Dutta, D.; Kumar, S. E-waste in Information and Communication Technology Sector: Existing scenario, management schemes and initiatives. Environ. Technol. Innov. 2022, 27, 102797. [Google Scholar] [CrossRef] [Scilit]
- Ghulam, S.T.; Abushammala, H. Challenges and opportunities in the management of electronic waste and its impact on human health and environment. Sustainability 2023, 15, 1837. [Google Scholar] [CrossRef] [Scilit]
- Shi, J.; Liu, S.; Zhang, L.; Yang, B.; Shu, L.; Yang, Y.; Ren, M.; Wang, Y.; Chen, J.; Chen, W. Smart textile-integrated microelectronic systems for wearable applications. Adv. Mater. 2020, 32, 1901958. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Wikipedia, Units of Textile Measurement. Available online: https://en.wikipedia.org/wiki/Units_of_textile_measurement (accessed on 7 December 2025).
- Stavrakis, A.K.; Simić, M.; Stojanović, G.M. Electrical characterization of conductive threads for textile electronics. Electronics 2021, 10, 967. [Google Scholar] [CrossRef] [Scilit]
- Badawi, N.M.; Batoo, K.M.; Hussain, S.; Agrawal, N.; Bhuyan, M.; Bashir, S.; Subramaniam, R.; Kasi, R. Design and Characterization of electroconductive graphene-coated cotton fabric for wearable electronics. Coatings 2023, 13, 1601. [Google Scholar] [CrossRef] [Scilit]
- Sfameni, S.; Lawnick, T.; Rando, G.; Visco, A.; Textor, T.; Plutino, M.R. Super-hydrophobicity of polyester fabrics driven by functional sustainable fluorine-free silane-based coatings. Gels 2023, 9, 109. [Google Scholar] [CrossRef] [Scilit]
- Berzowska, J.; Bromley, M. Soft computation through conductive textiles. In Proceedings of the International Foundation of Fashion Technology Institutes Conference, Toronto, ON, Canada, 12–14 April 2007; International Foundation of Fashion Technology Institutes: New Delhi, India, 2007; pp. 12–15. [Google Scholar]
- Vasile, S.; Deruck, F.; Hertleer, C.; De Raeve, A.; Ellegiers, T.; De Mey, G. Study of the contact resistance of interlaced stainless steel yarns embedded in hybrid woven fabrics. Autex Res. J. 2017, 17, 170–176. [Google Scholar] [CrossRef] [Scilit]
- AMANN Group. AMANN TechX Brochure. Available online: https://www.amann.com/fileadmin/user_upload/Download_Center/Brochures/AMANN_TechX_Brochure_EN.pdf (accessed on 25 April 2025).
- Coats. Coats Magellan. Available online: https://www.coats.com/en/products/threads/magellan/magellan/ (accessed on 25 April 2025).
- Elektrisola Feindraht AG. Textile Wire: Technical Brochure; Elektrisola Feindraht AG: Lucerne, Switzerland, 2015. [Google Scholar]
- Syscom Advanced Materials. Liberator™ 40; Syscom Advanced Materials: Columbus, OH, USA, 2018. [Google Scholar]
- Marciniak, K.; Grabowska, K.; Stempień, Z.; Ciesielska-Wrobel, I.; Rutkowska, A.; Taranek, D. Woven fabrics containing hybrid yarns for shielding electromagnetic radiation. Fibres Text. East. Eur. 2016, 24, 109–115. [Google Scholar] [CrossRef] [Scilit]
- Khan, A.U.A.; Saha, A.K.; Bristy, Z.T.; Tazrin, T.; Baqui, A.; Dev, B. Development of the smart jacket featured with medical, sports, and defense attributes using conductive thread and thermoelectric fabric. Eng. Proc. 2023, 30, 18. [Google Scholar]
- Zheng, Y.; Jin, L.; Qi, J.; Liu, Z.; Xu, L.; Hayes, S.; Gill, S.; Li, Y. Performance evaluation of conductive tracks in fabricating e-textiles by lock-stitch embroidery. J. Ind. Text. 2022, 51, 6864S–6883S. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.