


Abstract
4Cr13 martensitic stainless steel is widely used for plastic molds, but welding repair can produce heterogeneous weld/HAZ microstructures and a strength–toughness trade-off. This study evaluates how filler-wire composition and post-weld heat treatment affect the mechanical performance of repaired 4Cr13 steel. TIG welding was performed using high-molybdenum (HM), low-carbon (LC), and base-metal (BM) wires, followed by either post-weld tempering or quenching and tempering. Post-weld quenching and tempering reduced the hardness gradient and improved the overall hardness uniformity. The average weld-metal hardness followed HM > BM > LC, while the BM joint showed the smallest hardness variation because its nominal composition matched that of the base metal. After quenching and tempering, the tensile strengths of the HM, LC, and BM joints reached 1299.5, 1315.6, and 1300.0 MPa, respectively, compared with 1290.8 MPa for the similarly treated base metal. The corresponding impact energies were 58.9, 116.3, and 36.8 J, with LC showing the highest toughness. Fracture observations were consistent with these mechanical-property differences. The results demonstrate that filler-wire composition and post-weld heat-treatment route should be selected jointly according to the required balance of hardness uniformity, strength, ductility, and impact toughness, providing an experimental basis for repair-welding process selection for 4Cr13 steel.
1. Introduction
Due to its high strength, high hardness, and excellent wear and corrosion resistance, 4Cr13 martensitic stainless steel is widely used in high-end applications, including the manufacture of plastic molds, wear- and corrosion-resistant mechanical components, and petrochemical valves [1,2,3]. However, it exhibits a high carbon equivalent and a pronounced quench-hardening tendency [4]. When subjected to welding thermal cycles, coarse and brittle martensite forms in both the weld metal and the heat-affected zone (HAZ) [5,6], leading to increased residual stresses [7,8] and severe embrittlement of the HAZ [9]. Consequently, welded joints usually constitute the weakest region in terms of the mechanical performance of the entire structure, thereby severely restricting the engineering application of the material in large-scale and complex structures.
To date, extensive research has been conducted to improve the overall performance of welded joints by optimizing welding process parameters. Numerous studies have demonstrated that optimizing heat input and employing pulsed current can effectively suppress grain coarsening [10,11] and reduce the formation of network carbides [12], thereby improving the mechanical properties of welded joints. Extensive research has shown that post-weld heat treatment can improve the mechanical properties of welded joints, eliminate residual stresses [13,14], homogenize the microstructure, and reduce susceptibility to cold cracking [15,16]. Selecting an appropriate welding wire is also an effective approach to improving the performance of welded joints [17,18]. However, the selection of welding consumables has long been constrained by the strength–toughness trade-off [19,20]. The use of homogeneous martensitic welding wire ensures high hardness in the joint; however, its high-carbon content produces brittle, unquenched martensite [21], leading to a deterioration in joint performance. When a heterogeneous austenitic welding wire is used to prevent cracking, the resulting weld exhibits good ductility and toughness as well as high hydrogen solubility; however, its strength cannot match that of the base metal [22,23]. Consequently, optimizing the composition of welding consumables to suppress cold cracking while maintaining high joint strength remains a major challenge in this field.
To overcome this problem, recent research has increasingly focused on the development of martensitic welding consumables through optimization of the alloying element composition. Many researchers have attempted to improve weld ductility and toughness by reducing the carbon content of welding consumables [24,25] or by introducing alloying elements such as Cr and Mo to enhance joint mechanical properties [26]. Although current research has provided valuable insights into improving the mechanical properties of martensitic stainless steel welded joints, research on the selection of welding wires for 4Cr13 martensitic stainless steel remains limited.
Building on previous studies, this study selected three representative welding consumables for a comparative analysis of the synergistic effects of welding wire composition and post-weld heat treatment on the hardness distribution and overall mechanical properties of welded joints. A comparative analysis of fracture surface morphology after tensile and impact tests was also performed. The aim of this study is not only to identify the optimal combination of welding consumables and post-weld heat treatment that achieves the best overall performance, but also to provide theoretical guidance for high-quality welding and the safe, reliable service of 4Cr13 steel in complex industrial environments.
2. Materials and Methods
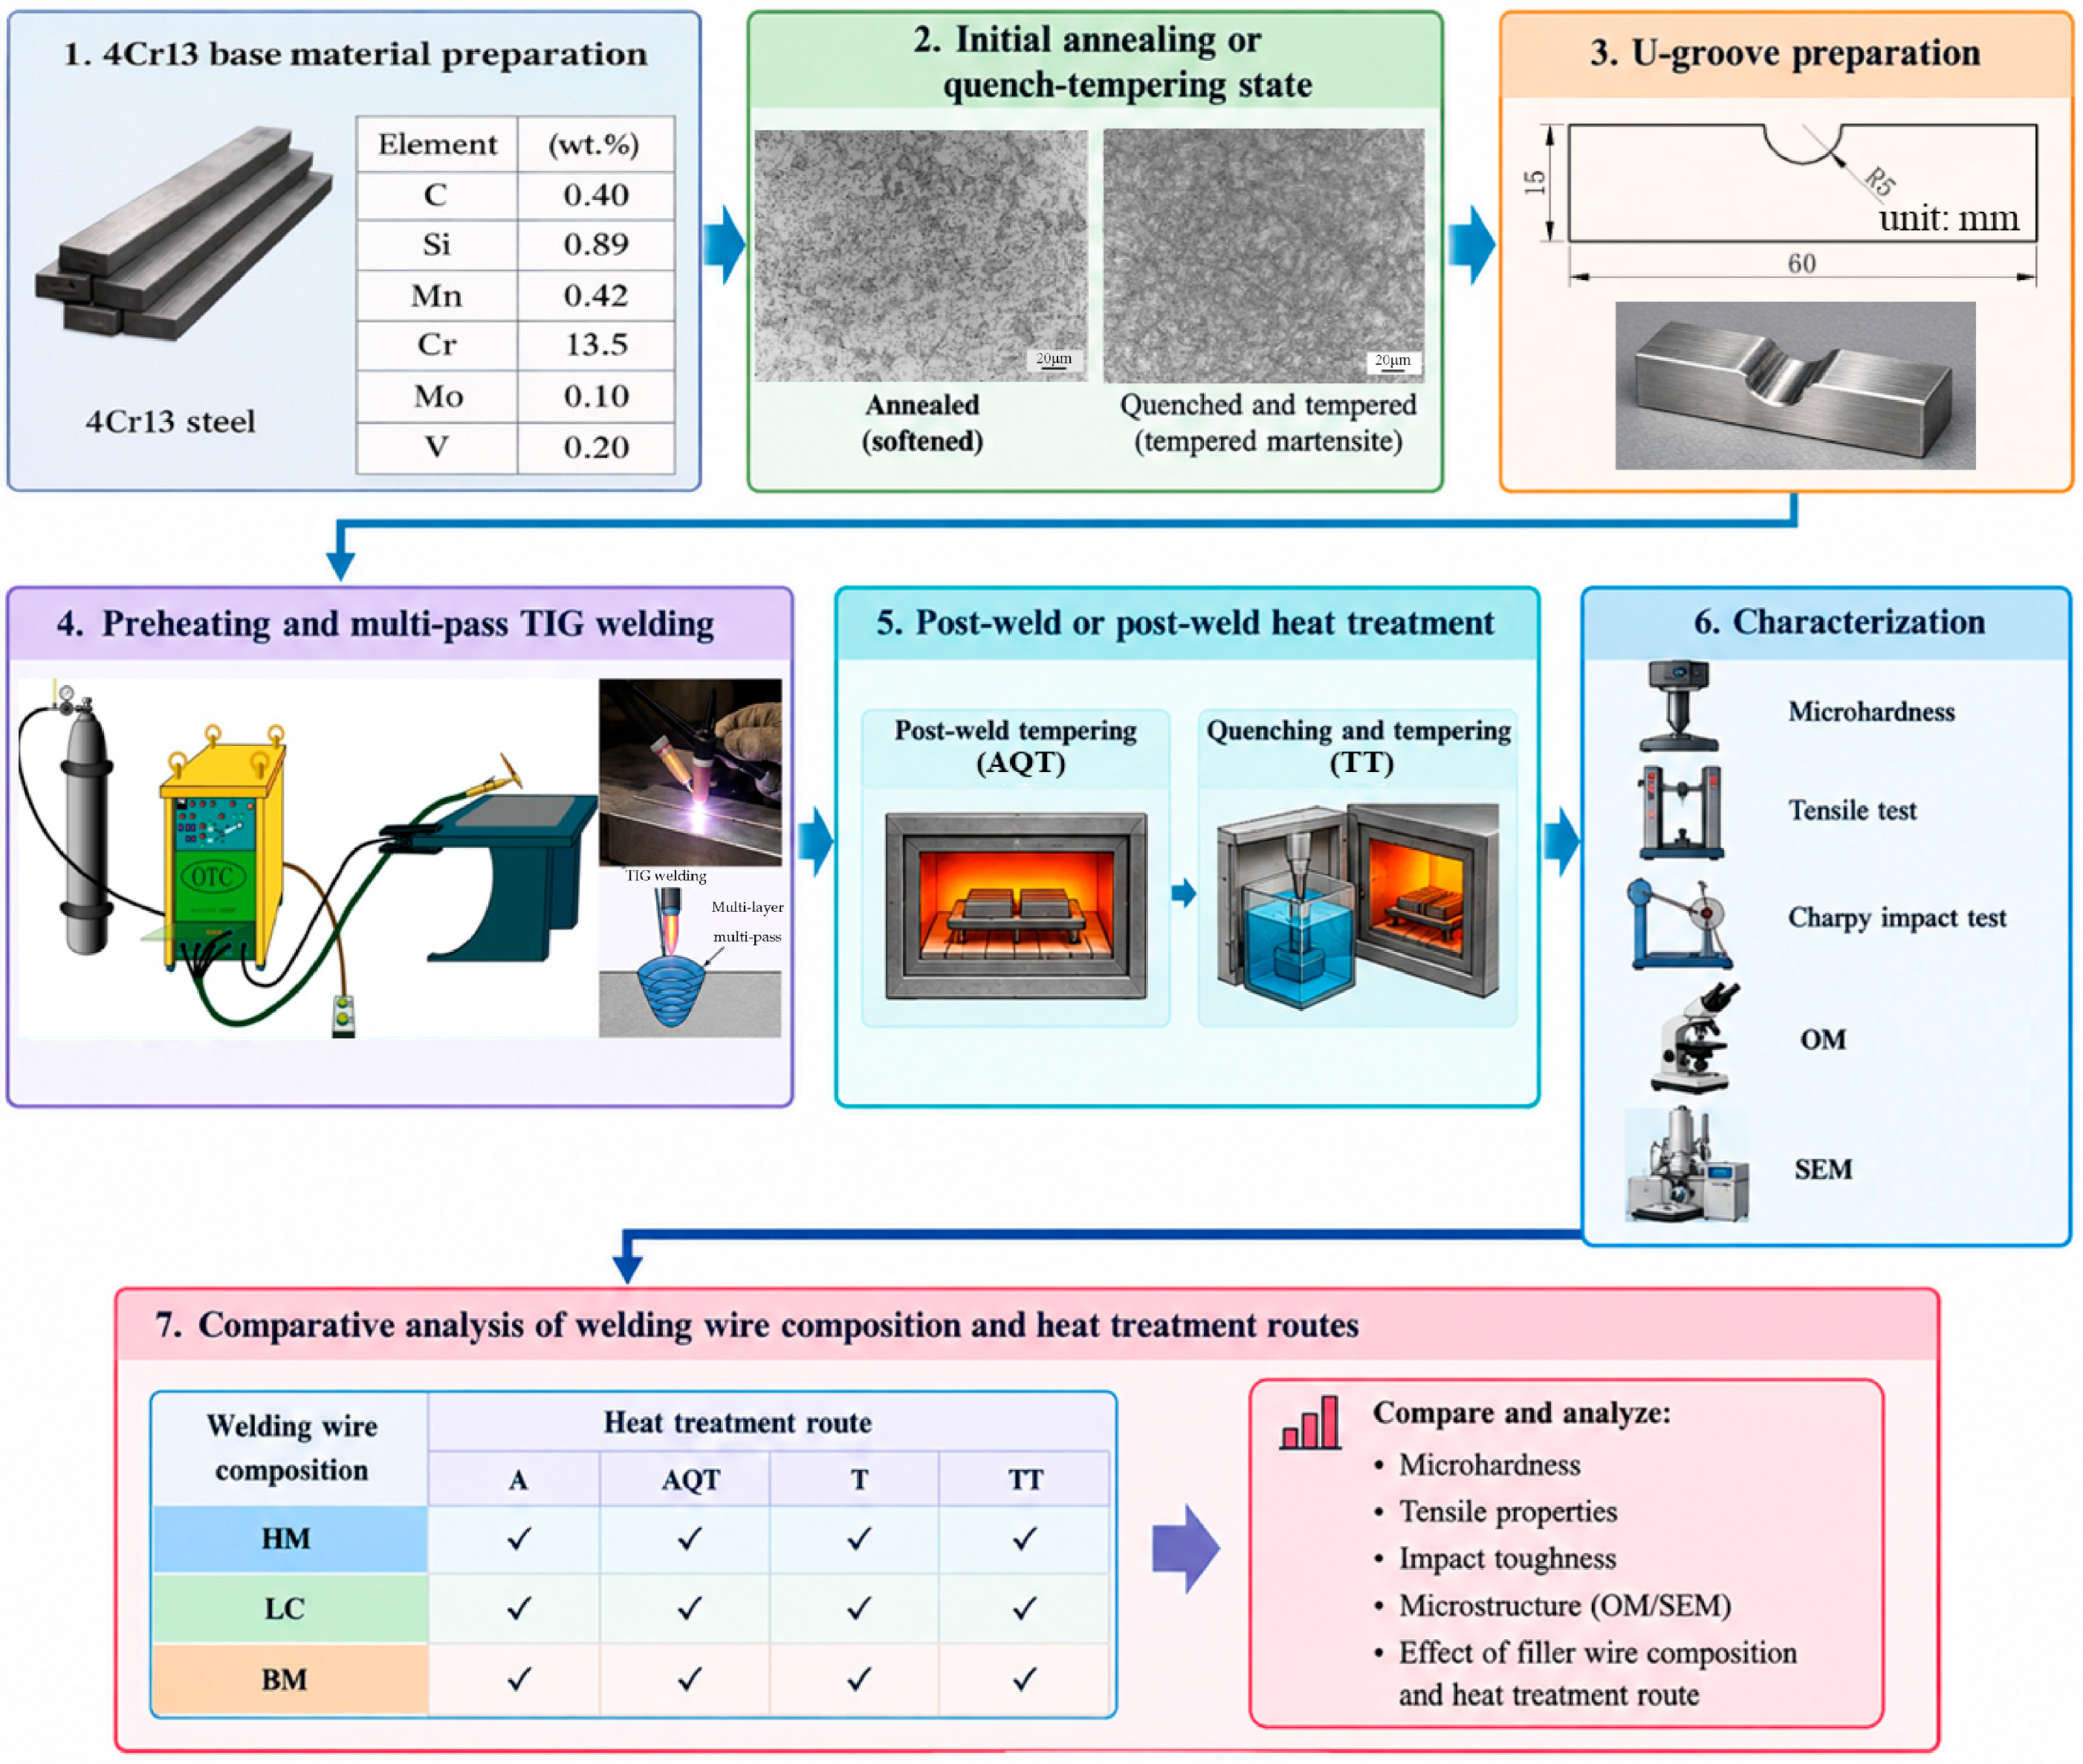
As shown in Figure 1, this study systematically investigated the effects of filler wire composition and post-weld heat treatment on the microstructure and mechanical properties of 4Cr13 steel welded joints. First, 4Cr13 base materials in the annealed and quenched-and-tempered conditions were prepared, followed by machining U-shaped grooves. Multi-layer, multi-pass TIG welding was then performed using three types of filler wires, namely high-molybdenum (HM), low-carbon (LC), and base-metal (BM). All welding wires had a diameter of 1.6 mm. Different post-weld heat-treatment routes, including post-weld tempering and quenching–tempering, were subsequently applied to establish a comparative experimental system involving different filler wire compositions and heat-treatment conditions. The welded joints were characterized in terms of microhardness, tensile properties, and Charpy impact toughness, while optical microscopy (OM, MA100, Nikon, Tokyo, Japan) and scanning electron microscopy (SEM, Supra 40, Zeiss, Oberkochen, Germany) were employed to examine microstructure and fracture morphology. Finally, a comparative analysis of hardness distribution, strength, ductility, impact toughness, microstructure, and fracture behavior were conducted to clarify the effects of filler wire composition and post-weld heat treatment on the overall performance of 4Cr13 steel welded joints, thereby providing an experimental basis for the selection of filler wires and optimization of post-weld heat-treatment procedures for welding repair of 4Cr13 steel.
Figure 1.
Experimental workflow of the study: A–Annealed base material, as-welded; AQT–Annealed base material, quenched and tempered after welding; T–Tempered base material, as-welded; TT–Tempered base material, tempered after welding.
2.1. Materials and Specimen Preparation
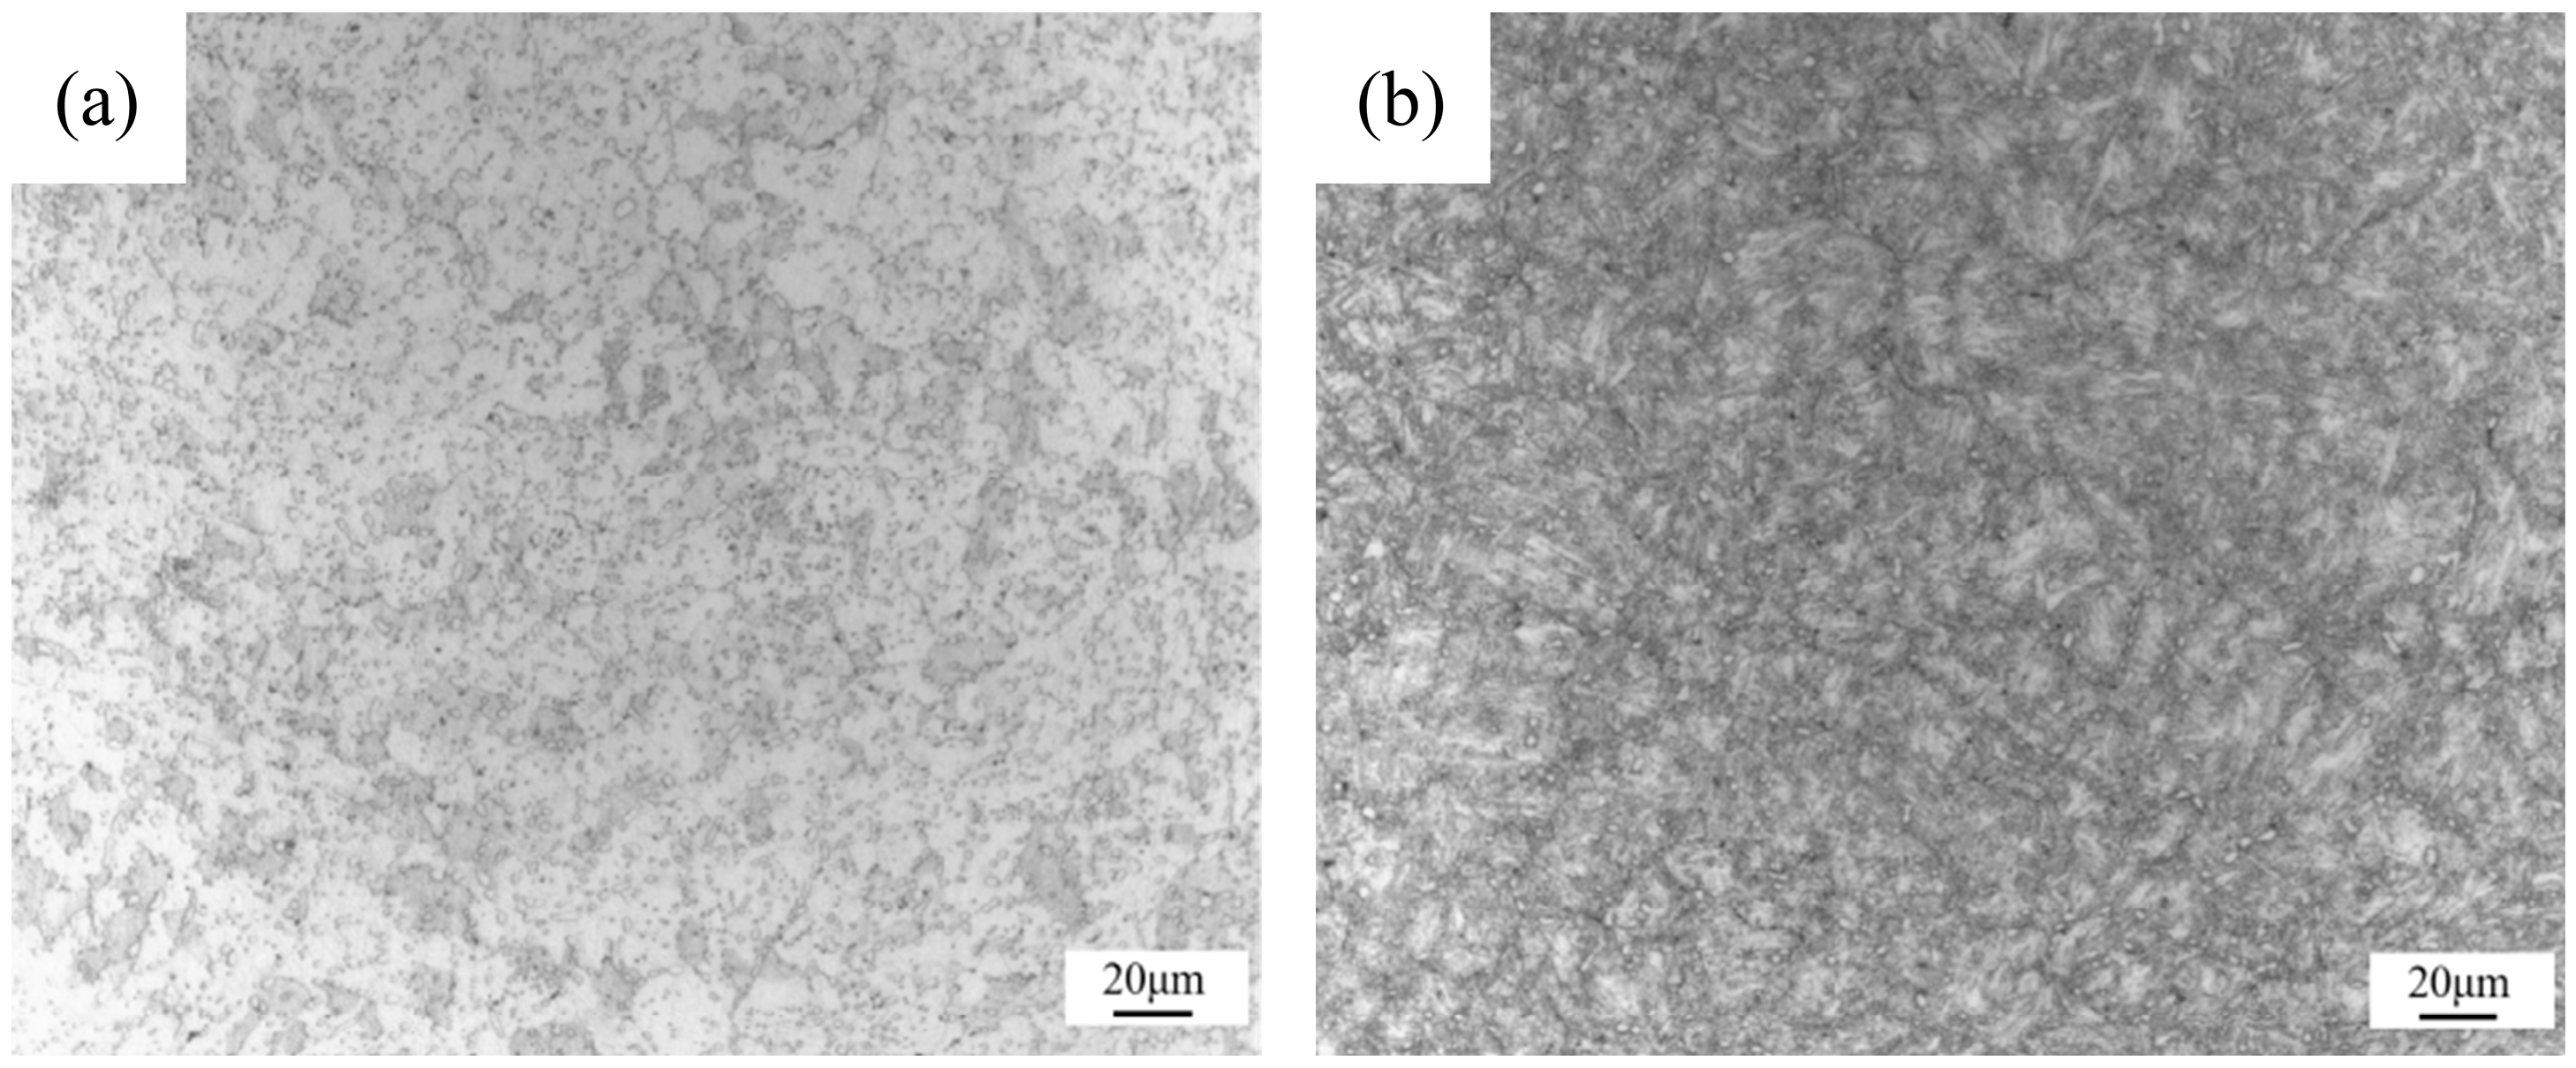
The chemical compositions of the base metal and the welding wires are shown in Table 1. Figure 2 shows the microstructure of 4Cr13 steel in different heat-treated conditions. In the annealed condition, the microstructure consists of granular pearlite, as shown in Figure 2a, with a hardness of 188 HBW; this was used as the annealed base metal for welding tests. Figure 2b shows the microstructure of 4Cr13 steel after quenching and tempering. Annealed 4Cr13 steel was quenched at 1030 °C and tempered twice at 520 °C to achieve a hardness of 46.0–48.0 HRC. The resulting microstructure consisted of tempered martensite, and the tempered material was used as the base metal for the subsequent welding experiments.
Table 1.
Chemical composition (wt.%) of base metal and welding wire.
Figure 2.
Microstructure of 4Cr13 under different heat treatment conditions: (a) annealed; (b) tempered.
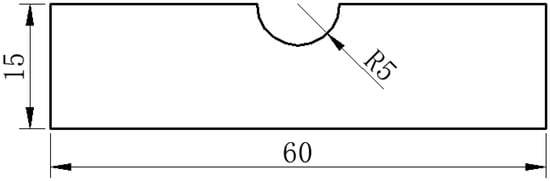
Prior to welding, a U-shaped groove is machined into the base metal surface using wire cutting; the groove profile and dimensions are shown in Figure 3. Welding was performed using a tungsten inert gas (TIG) welding machine (YC-400TX, Tangshan Panasonic Industrial Machinery Co., Ltd., Tangshan, China)operating in direct current electrode negative (DCEN) mode. The groove was filled using a multi-layer, multi-pass welding procedure. The specimens were preheated to 300 °C and held for 2 h prior to welding. The welding current was 100 A, the inter-pass temperature was maintained at 200–250 °C, and the argon flow rate was 15 L/min.
Figure 3.
Schematic diagram of the welding groove (unit: mm).
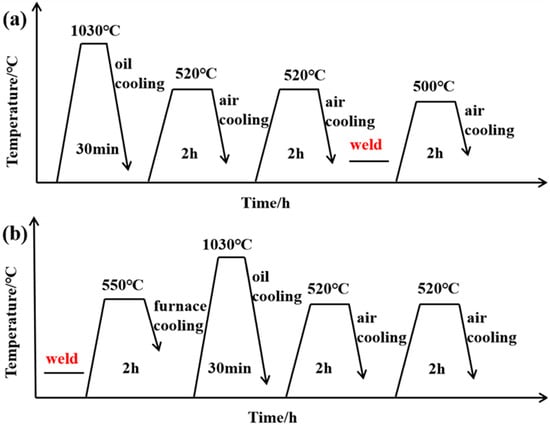
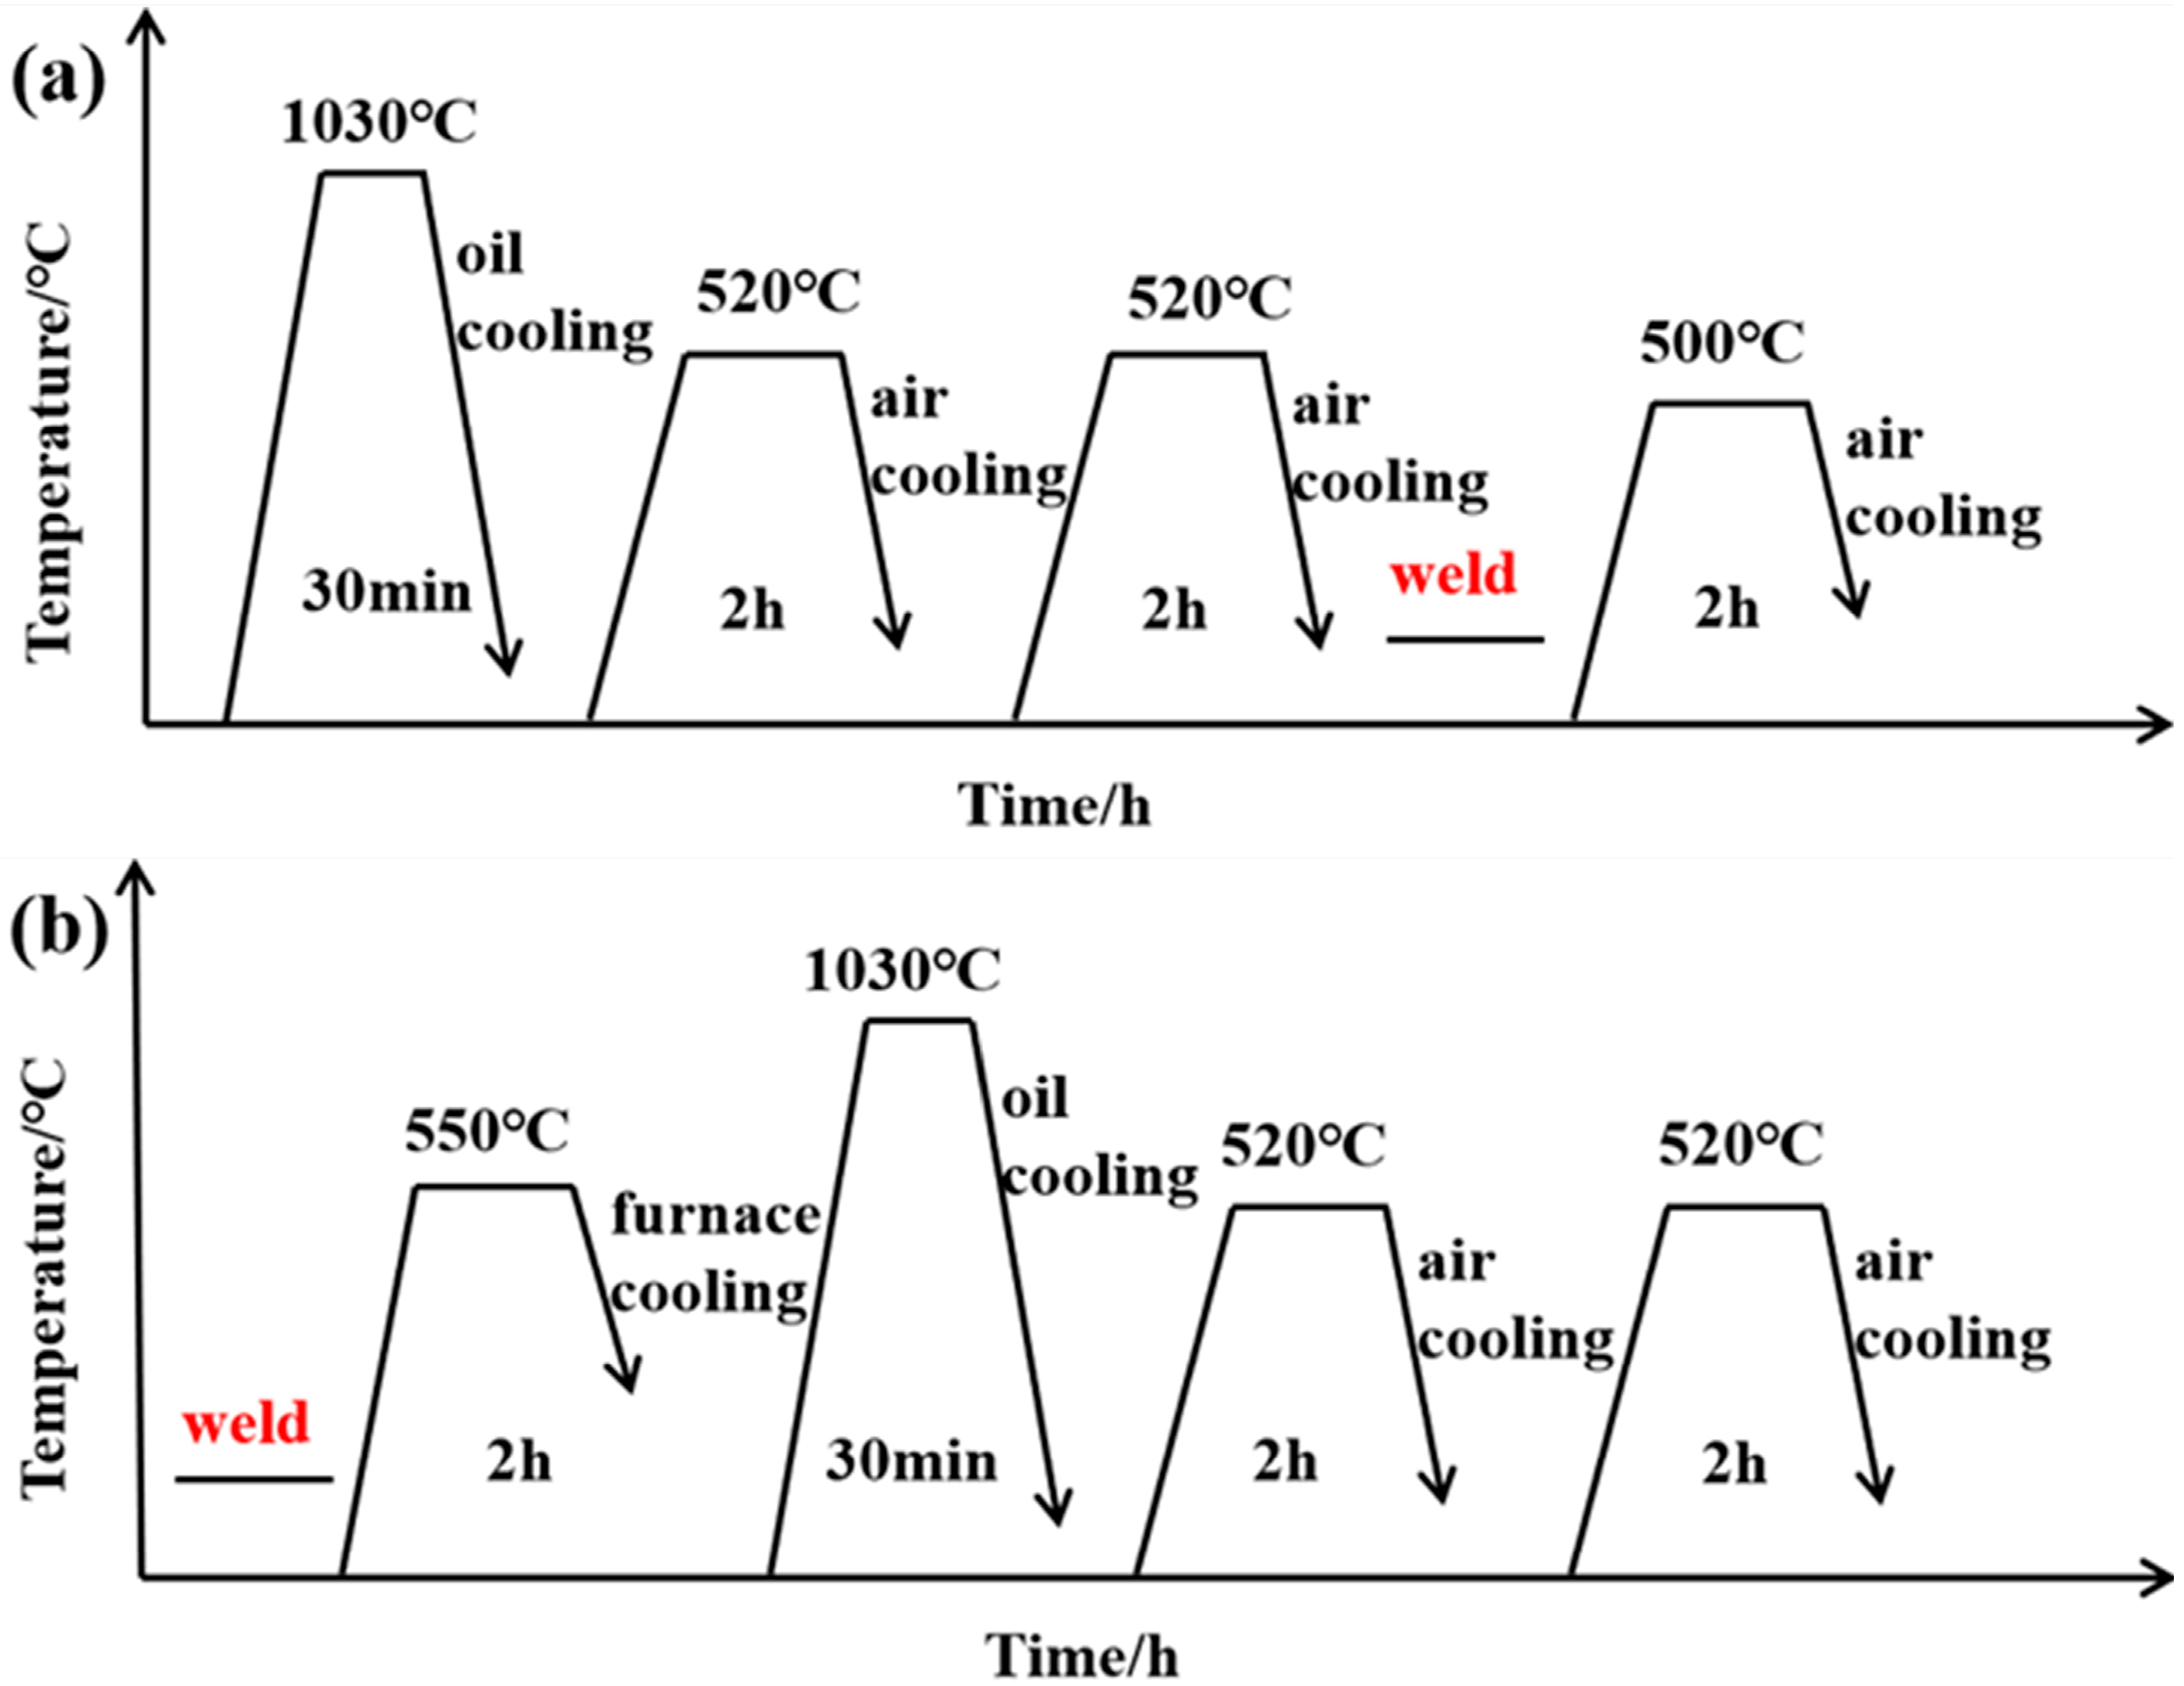
To better represent practical industrial welding repair conditions, two different processing routes were designed by considering both the initial condition of the 4Cr13 base material and the post-weld heat treatment procedure. The base material in the tempered condition was quenched and tempered prior to welding and was tempered again after welding. Following post-weld stress-relief treatment, the annealed base material was quenched and tempered using the same heat-treatment schedule as that applied to the tempered base material. The overall welding and heat-treatment procedures are shown in Figure 4. Based on the heat-treatment condition of the base material prior to welding and the post-weld heat-treatment procedure, the test specimens were designated as follows: annealed base material, as-welded (A); annealed base material, quenched and tempered after welding (AQT); tempered base material, as-welded (T); and tempered base material, tempered after welding (TT). To clarify the experimental design, the specimens were divided according to both the base-metal condition before welding and the heat treatment after welding. The T and TT groups were welded using tempered 4Cr13 steel as the initial base material, whereas the A and AQT groups were welded using annealed 4Cr13 steel. T and A represent the corresponding as-welded conditions, while TT and AQT represent post-weld tempering and post-weld quenching-and-tempering routes, respectively. Therefore, the comparison between TT and AQT represents two practical repair routes involving different initial microstructures and different post-weld heat treatments rather than an isolated comparison of post-weld heat treatment. The effects of post-weld treatment are therefore discussed primarily within each initial base-metal condition.
Figure 4.
Welding and heat treatment process diagram: (a) tempering after welding (TT); (b) quenching and tempering after welding (AQT).
2.2. Experimental Methods
The hardness of the welded joints was measured using an micro-Vickers hardness tester (HVS-1000M, Shanghai Johoyd Instrument Manufacture Co., Ltd., Shanghai, China) according to GB/T 4340.1—2024 [27] (‘Metallic materials—Vickers hardness test—Part 1: Test method’) using a load of 200 g with a dwell time of 10 s. The point located 1 mm below the weld surface was selected as the starting position for microhardness measurements. Measurements were then performed at intervals of 0.4 mm to determine the variation in microhardness from the weld metal to the base metal.
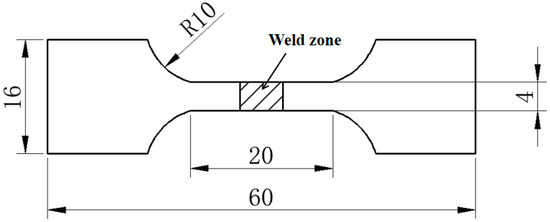
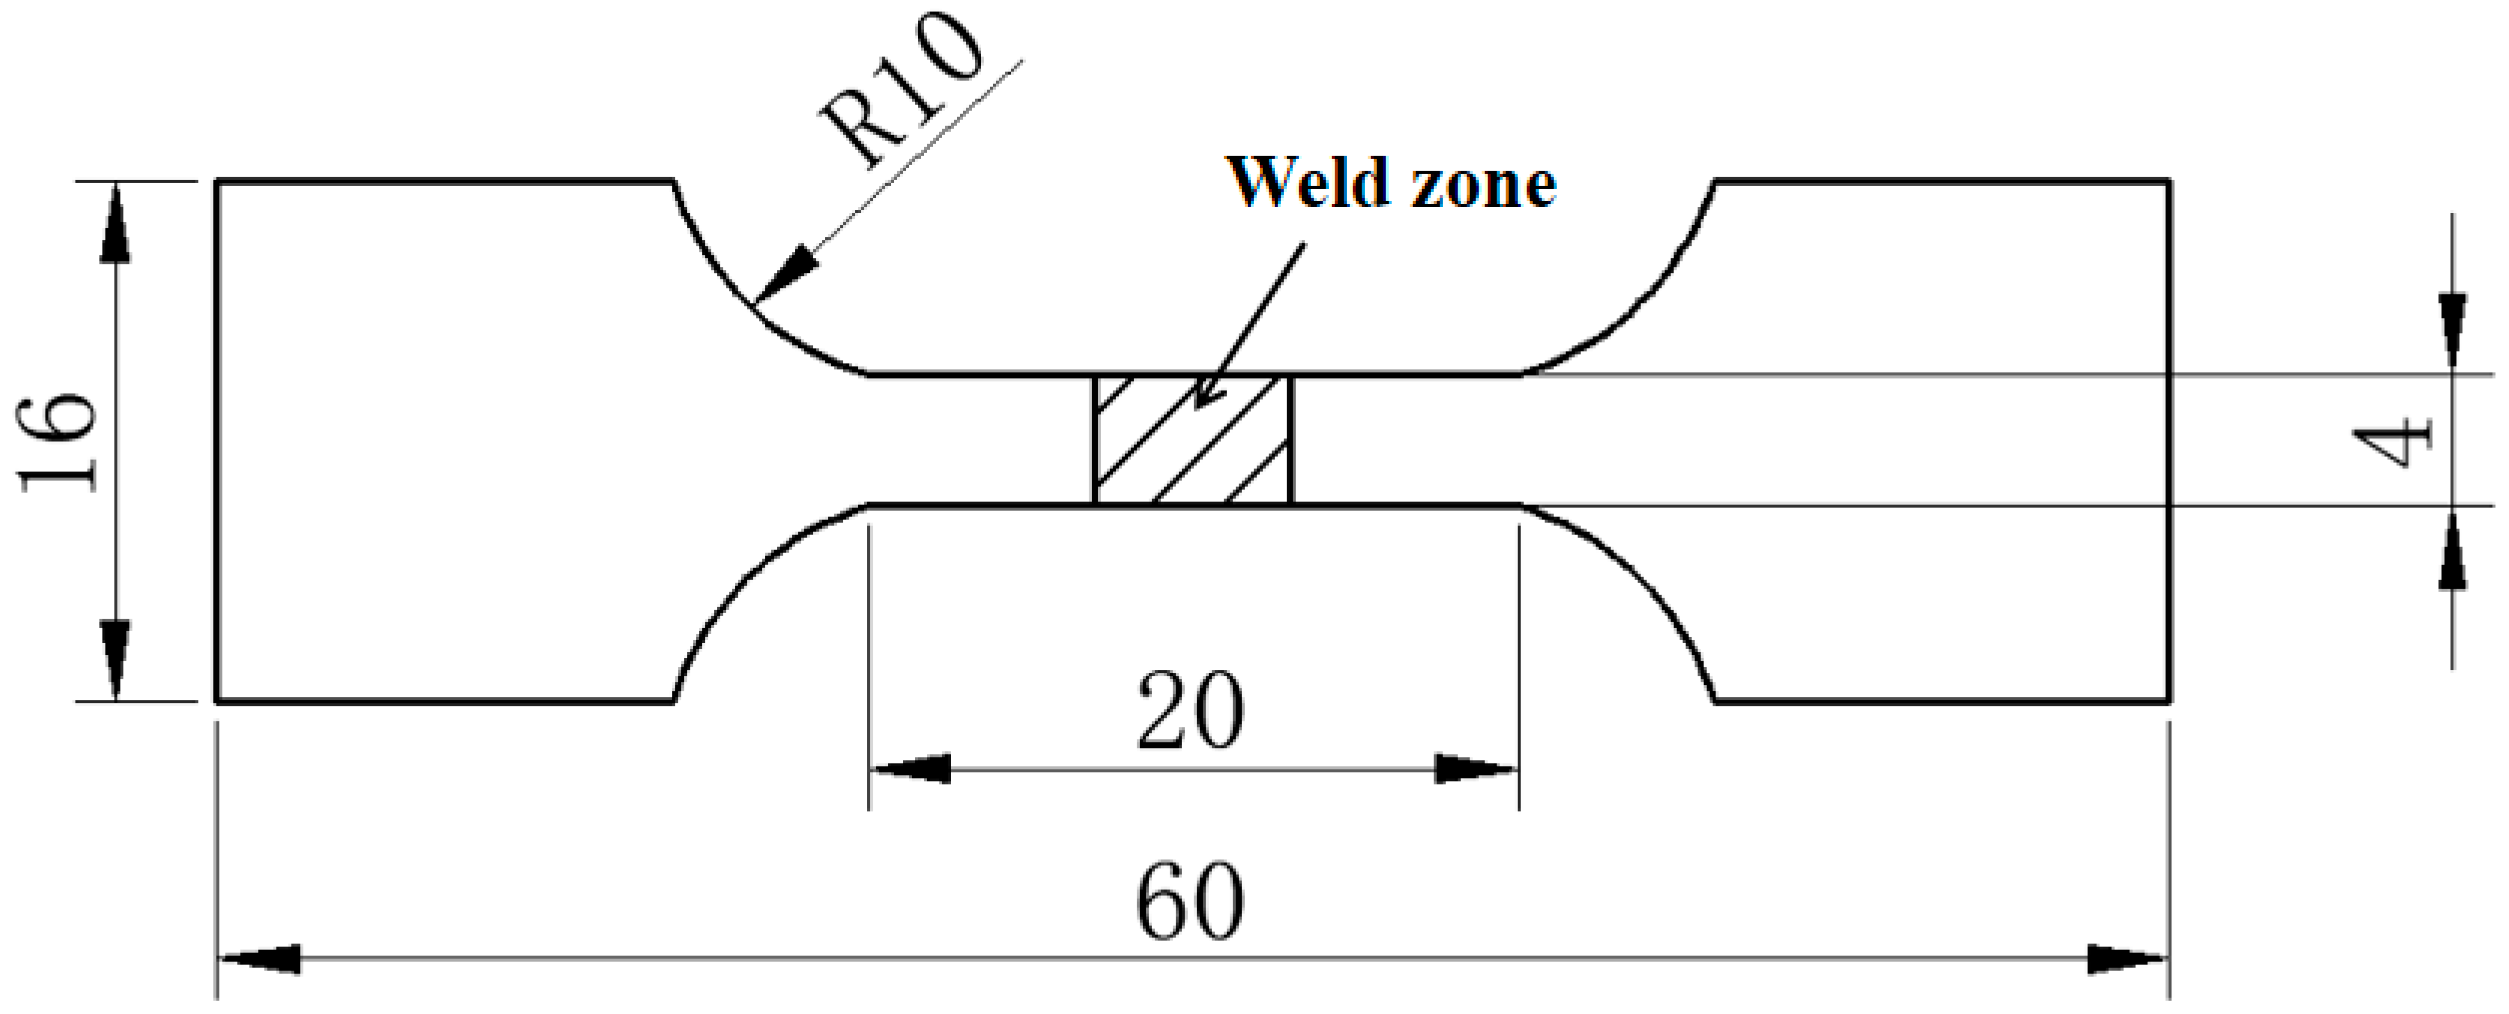
Flat tensile specimens were cut perpendicular to the weld centerline using a wire-cut machine, at a position 1 mm from the weld surface. The specimen dimensions are shown in Figure 5. The plate thickness is 2 mm. An microprocessor-controlled electronic universal testing machine (C45, MTS, Shanghai, China) was used for tensile testing of the welded joints in accordance with the GB/T 228.1-2021 [28] standard (‘Metallic materials—Tensile testing—Part 1: Method of test at room temperature’). Test two samples per group and ensure that the difference between the two test values is less than 10%; otherwise, conduct additional tests. After tensile testing, the cross-sections of the fractured specimens were etched using an aqueous FeCl3 solution containing hydrochloric acid. The fracture surfaces were examined using a ultra-deep-field 3D microscope (VHX-600, Keyence (China) Co. Ltd., Shanghai, China), while the microstructure adjacent to the fracture surfaces was observed using an metallurgical microscope (OM, Axio Lab. A1, Zeiss, Oberkochen, Germany). The tensile fracture morphologies were further characterized using a scanning electron microscope (SEM, Supra 40, Zeiss, Oberkochen, Germany).
Figure 5.
Tensile specimen (unit: mm).
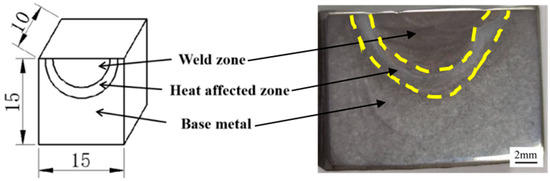
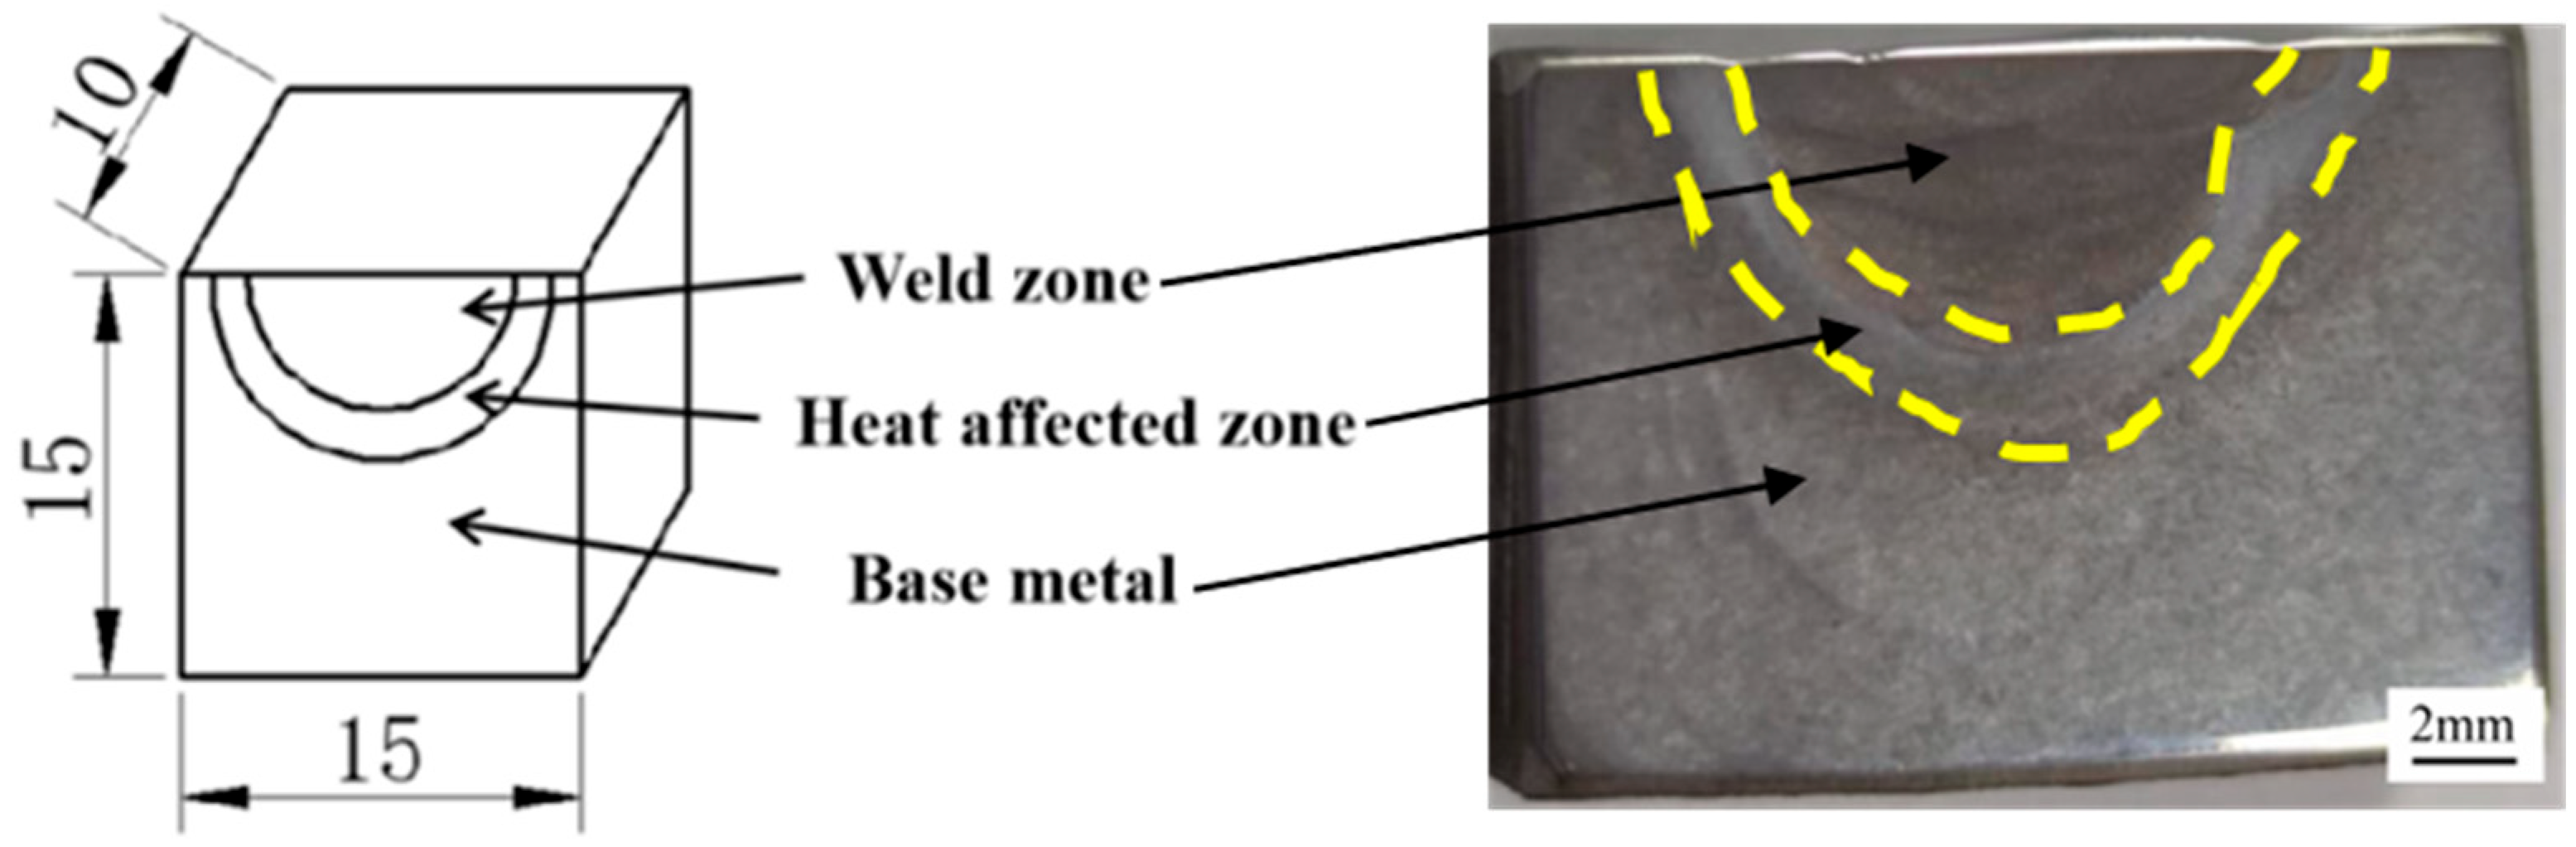
Charpy impact tests were performed on the welded specimens using an Charpy impact testing machine (ZBC2602-CE, MTS, Shanghai, China) according to GB/T 229—2020 [29] (‘Metallic materials—Charpy pendulum impact test method’). A pendulum energy of 300 J was used, and the specimen dimensions were 10 mm × 10 mm × 55 mm, with the weld located at the center of the specimen, as shown in Figure 6. Test 3 samples in each group and calculate the average. The impact load was applied perpendicular to the weld centerline. The absorbed impact energy reflected the combined effects of the weld metal and HAZ on the impact toughness of the specimen, thereby simulating variation in mold performance under impact loading after practical welding repair. After impact testing, the cross-sections of the fractured specimens were ground and polished, then etched using an aqueous FeCl3 solution containing hydrochloric acid. The microstructure adjacent to the impact fracture surface was examined using an metallographic microscope (OM, Axio Lab. A1, Zeiss, Oberkochen, Germany). The impact fracture surface morphology was examined using a ultra-deep-field 3D microscope (VHX-600, Keyence (China) Co. Ltd., Shanghai, China) and a scanning electron microscope (SEM, Supra 40, Zeiss, Oberkochen, Germany).
Figure 6.
Metallographic observation of welded joint (unit: mm).
3. Results
3.1. Microhardness
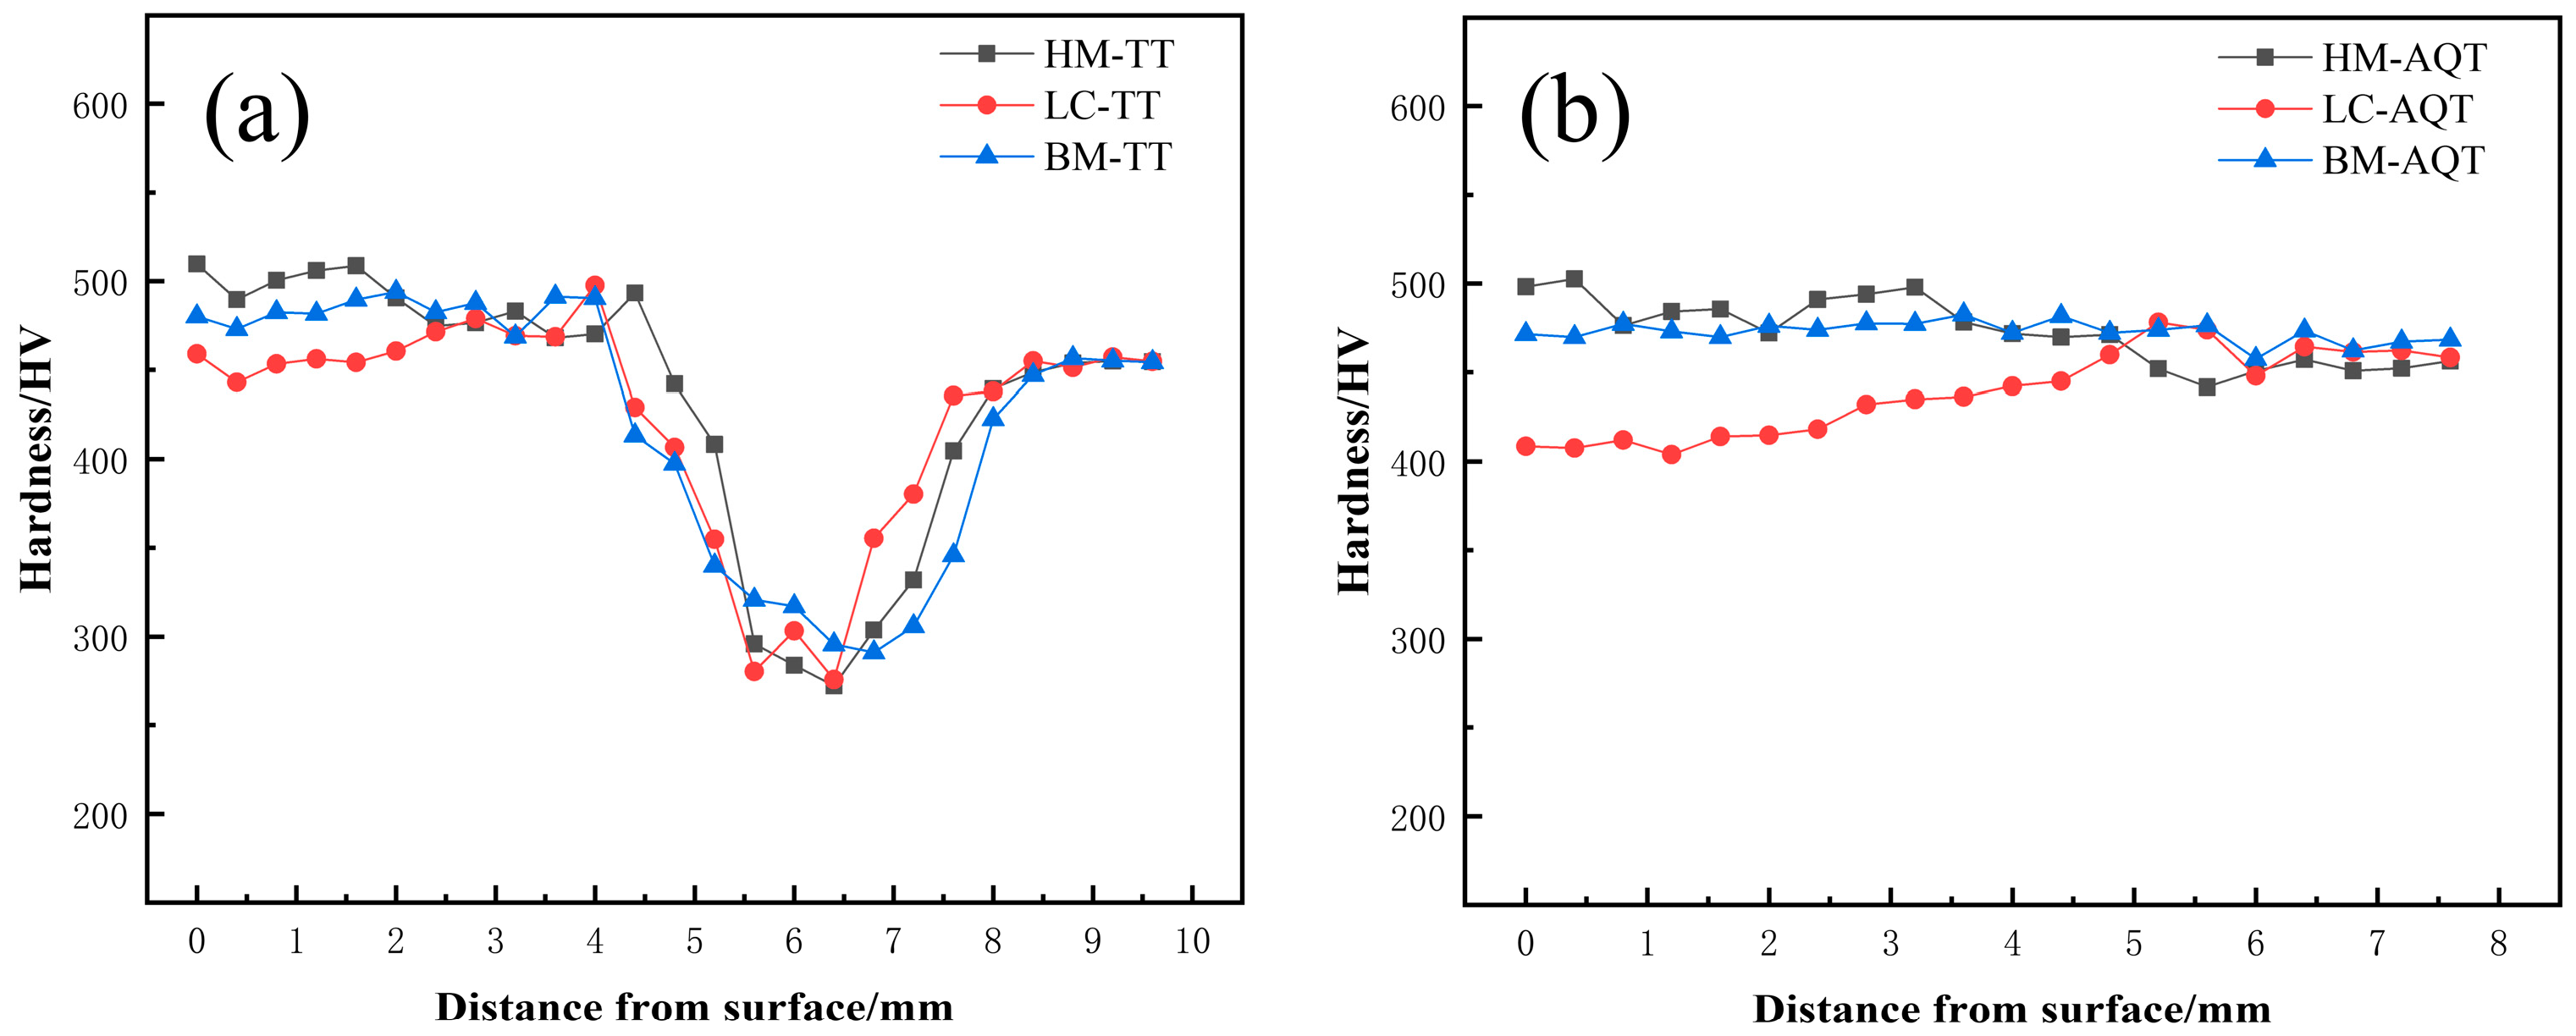
Figure 7 shows the microhardness distributions of the welded joints fabricated with different welding wires. As shown in Figure 7a, the microhardness profiles of the three welded joints exhibit similar trends, with all profiles showing a hardness valley. This behavior is attributed to the formation of a temper-softened zone in the HAZ, where the hardness is lower than that of the base material [30]. Figure 7b shows the microhardness profile of the annealed base material subjected to post-weld quenching and tempering. Compared with Figure 7a, the variation in microhardness is reduced. A comparative analysis revealed that, under the same heat treatment conditions, the hardness values of the HAZ and base material were essentially consistent among the three welding wires, whereas the hardness of the weld metal differed, with the average hardness following the order HM > BM > LC. After post-weld quenching and tempering, the hardness of the HM weld metal was higher than that of the base material, whereas the BM weld metal exhibited a hardness comparable to that of the base material. In contrast, the hardness of the LC weld metal was lower than that of the base material. This is primarily attributed to differences in the chemical compositions of the three welding wires. The higher hardness of the HM weld metal is associated with its relatively higher Mo content compared with the LC and BM welding wires. Previous studies have reported that Mo can contribute to strengthening in Fe-based weld metals [31,32]. BM welding wire has the same chemical composition as the base material; after post-weld quenching and tempering, the hardness values of the weld metal and base material are essentially identical. LC welding wire contains a relatively low carbon content, which may reduce both carbon solid solution strengthening and carbide precipitation strengthening; consequently, the weld metal exhibits lower hardness after heat treatment [33].
Figure 7.
Hardness gradient of welded joints with different welding wires: (a) tempering of tempered base metal after welding; (b) quenching and tempering of annealed base metal after welding.
To better compare the variations in microhardness distribution among different welded joints, a quantitative method based on the evaluation principle for repairing circular pits in mold steel [34] was introduced. The hardness fluctuation coefficient was used to assess the hardness uniformity of 4Cr13 steel welded joints, as shown in Equation (1):
where is the hardness fluctuation coefficient; is the maximum hardness of the welded joint; is the minimum hardness of the welded joint; and is the hardness of the base material. The smaller the differences between the maximum and minimum hardness values within the welded joint and the base material hardness, the lower the hardness fluctuation coefficient. This indicates better hardness uniformity and improved welding repair quality. The smaller the difference between the maximum and minimum hardness values within the welded joint relative to the hardness of the base material, the lower the hardness fluctuation coefficient. This indicates better hardness uniformity and higher welding repair quality. The specific hardness variations for the three types of welding wire in their respective heat-treated conditions are shown in Table 2, Table 3 and Table 4. It can be observed that, following post-weld tempering of the HM welded joint fabricated from tempered base material, the hardness difference within the welded joint (i.e., the difference between the maximum and minimum hardness values) decreased from 283 HV to 238 HV, while the hardness fluctuation coefficient decreased from 0.46 to 0.42. A similar trend was observed for the LC and BM welded joints after post-weld tempering; the hardness fluctuation coefficient decreased from 0.42 to 0.40 for LC and from 0.46 to 0.37 for BM, indicating that post-weld tempering improves hardness uniformity in 4Cr13 steel welded joints. After post-weld quenching and tempering of the annealed base material, the hardness difference between the HAZ and the base material was virtually eliminated. Meanwhile, the hardness difference within the welded joint was reduced, and the hardness fluctuation coefficient decreased. The three types of welding wire showed the same pattern of hardness variation, with coefficients of variation in hardness of 0.11, 0.12, and 0.04, respectively. A comparative study of the two post-weld heat treatment processes showed that, compared with post-weld tempering, post-weld quenching and tempering produced welded joints with lower hardness fluctuations. Among the three welding wires, the BM welded joint, owing to its chemical composition being consistent with that of the base material, exhibited hardness variations within ±10 HV of the base material hardness after post-weld quenching and tempering, demonstrating the best hardness uniformity.
Table 2.
Hardness fluctuation of welded joints of HM welding wire in different heat treatment states.
Table 3.
Hardness fluctuation of welded joints of LC welding wire in different heat treatment states.
Table 4.
Hardness fluctuation of welded joints of BM welding wire in different heat treatment states.
3.2. Tensile Properties
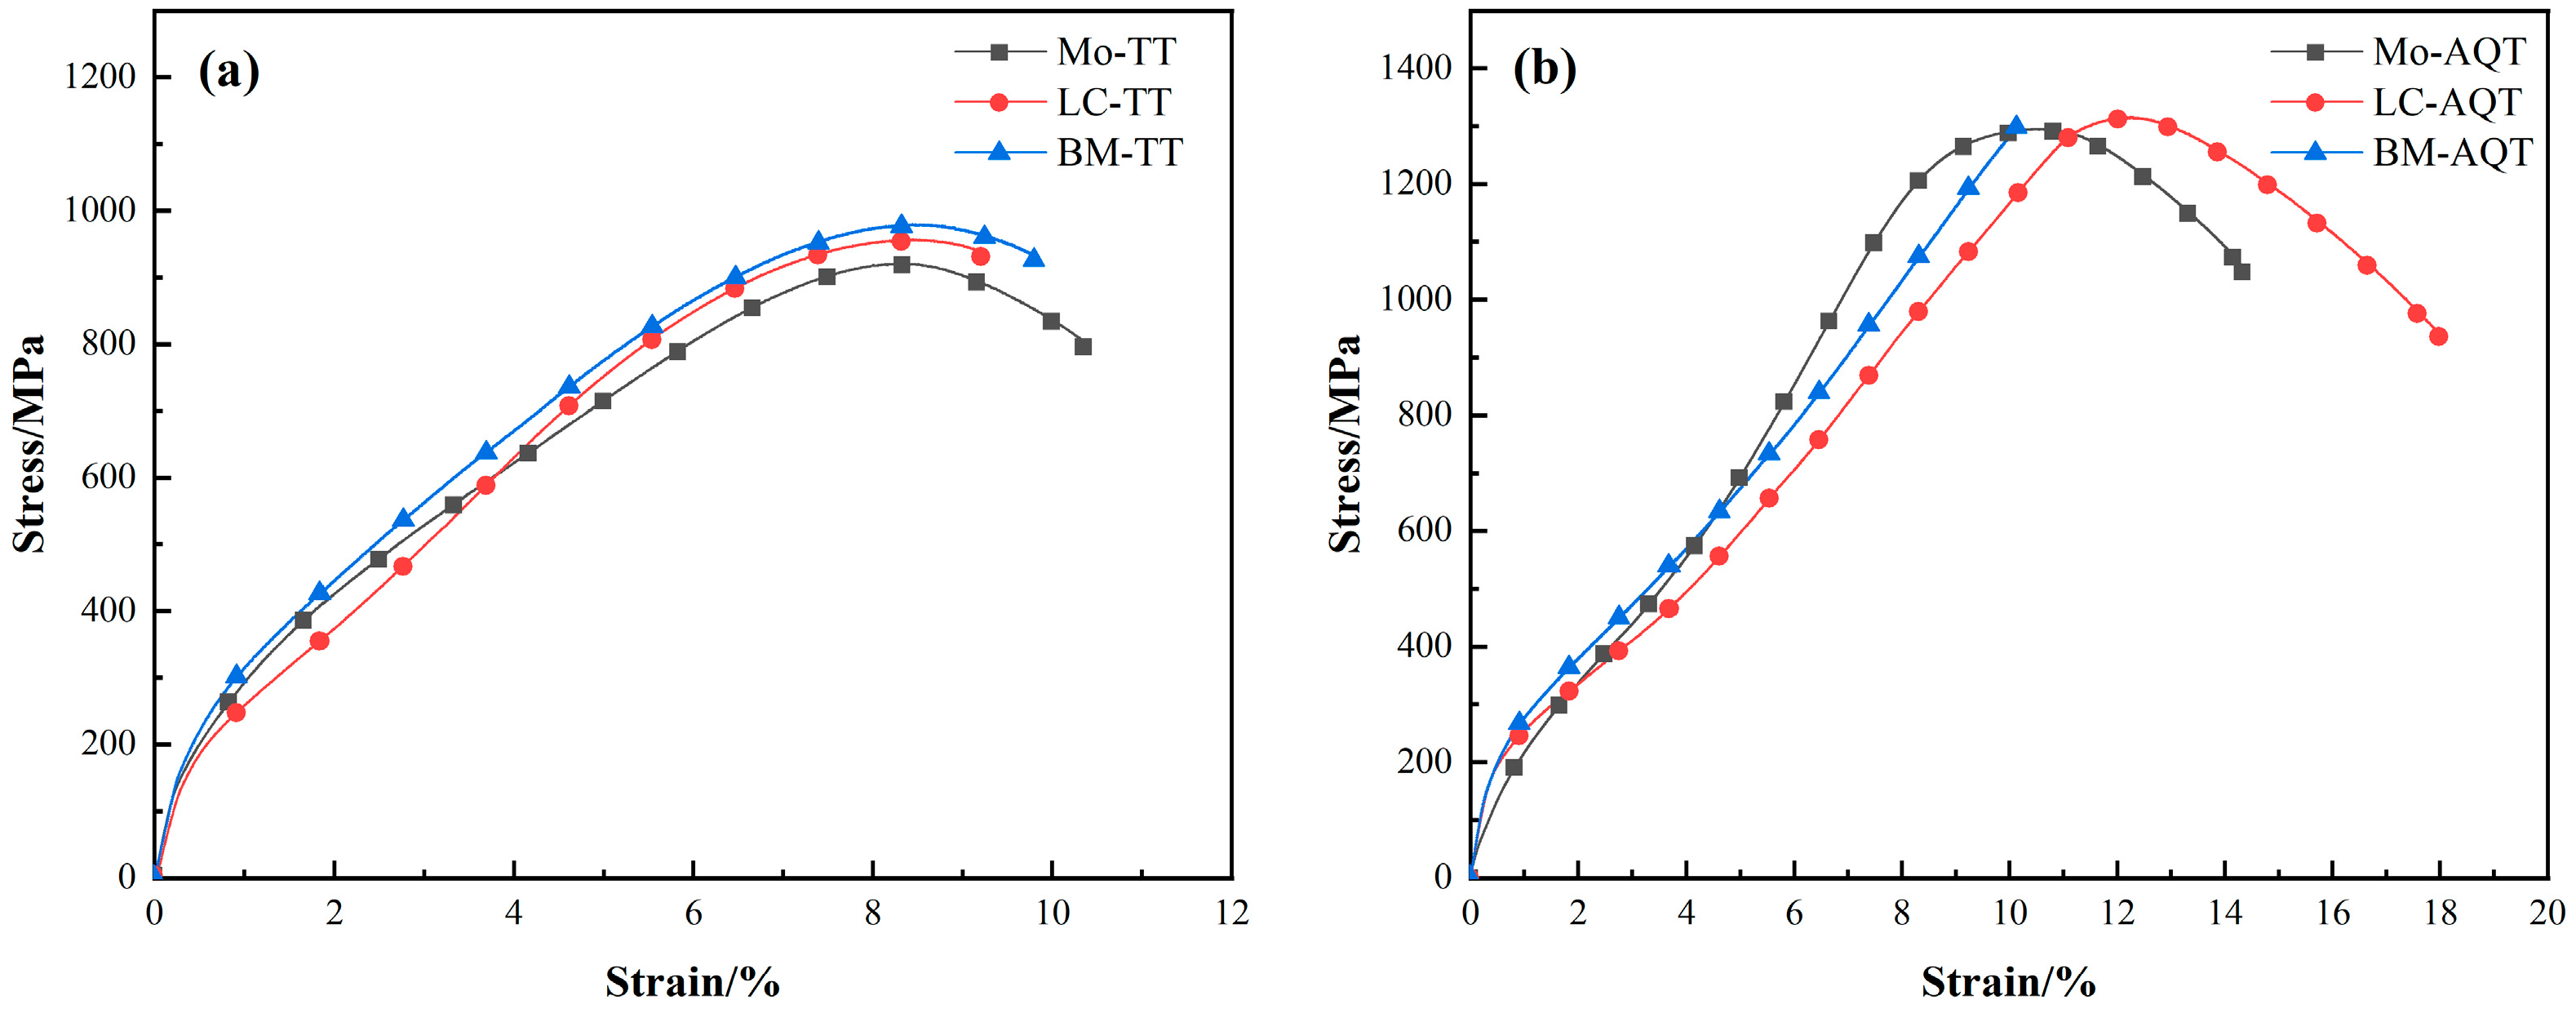
From the stress–strain curves of the welded joints for different welding wires under the same post-weld heat treatment process shown in Figure 8, it can be concluded that the tensile strength of the welded joints for the three types of welding wire is essentially the same. Table 5 presents the tensile test results of the welded joints. The tensile properties reported in Table 5 are individual representative measurement values, selected according to the actual data. After post-weld tempering, the tensile strengths of the welded joints fabricated with HM, LC, and BM welding wires were 920.9 MPa, 950.7 MPa, and 979.4 MPa, respectively, while their elongation values were 9.2%, 8.2%, and 8.6%, respectively, indicating that the elongation values were broadly comparable. Following post-weld quenching and tempering treatment, the tensile strengths of the welded joints fabricated with HM, LC, and BM welding wires were essentially identical, at 1299.5 MPa, 1315.6 MPa, and 1300.0 MPa, respectively. However, differences were observed in their elongation at break, which were 13.1%, 16.3%, and 8.9%, respectively. The LC welded joint exhibited the highest elongation at break, whereas the BM welded joint showed the lowest. The tensile strength of the base material subjected to the same quenching and tempering treatment was 1290.8 MPa.
Figure 8.
Stress–strain curves of welded joints with different welding wires: (a) tempering of tempered base metal after welding; (b) quenching and tempering of annealed base metal after welding.
Table 5.
Tensile results of the welded joints.
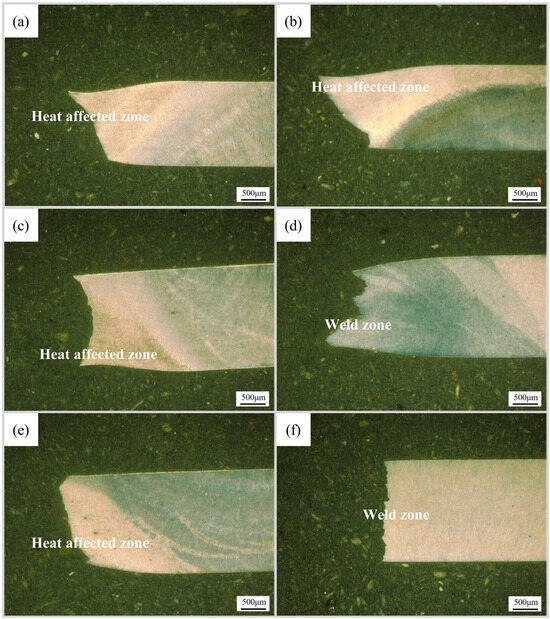
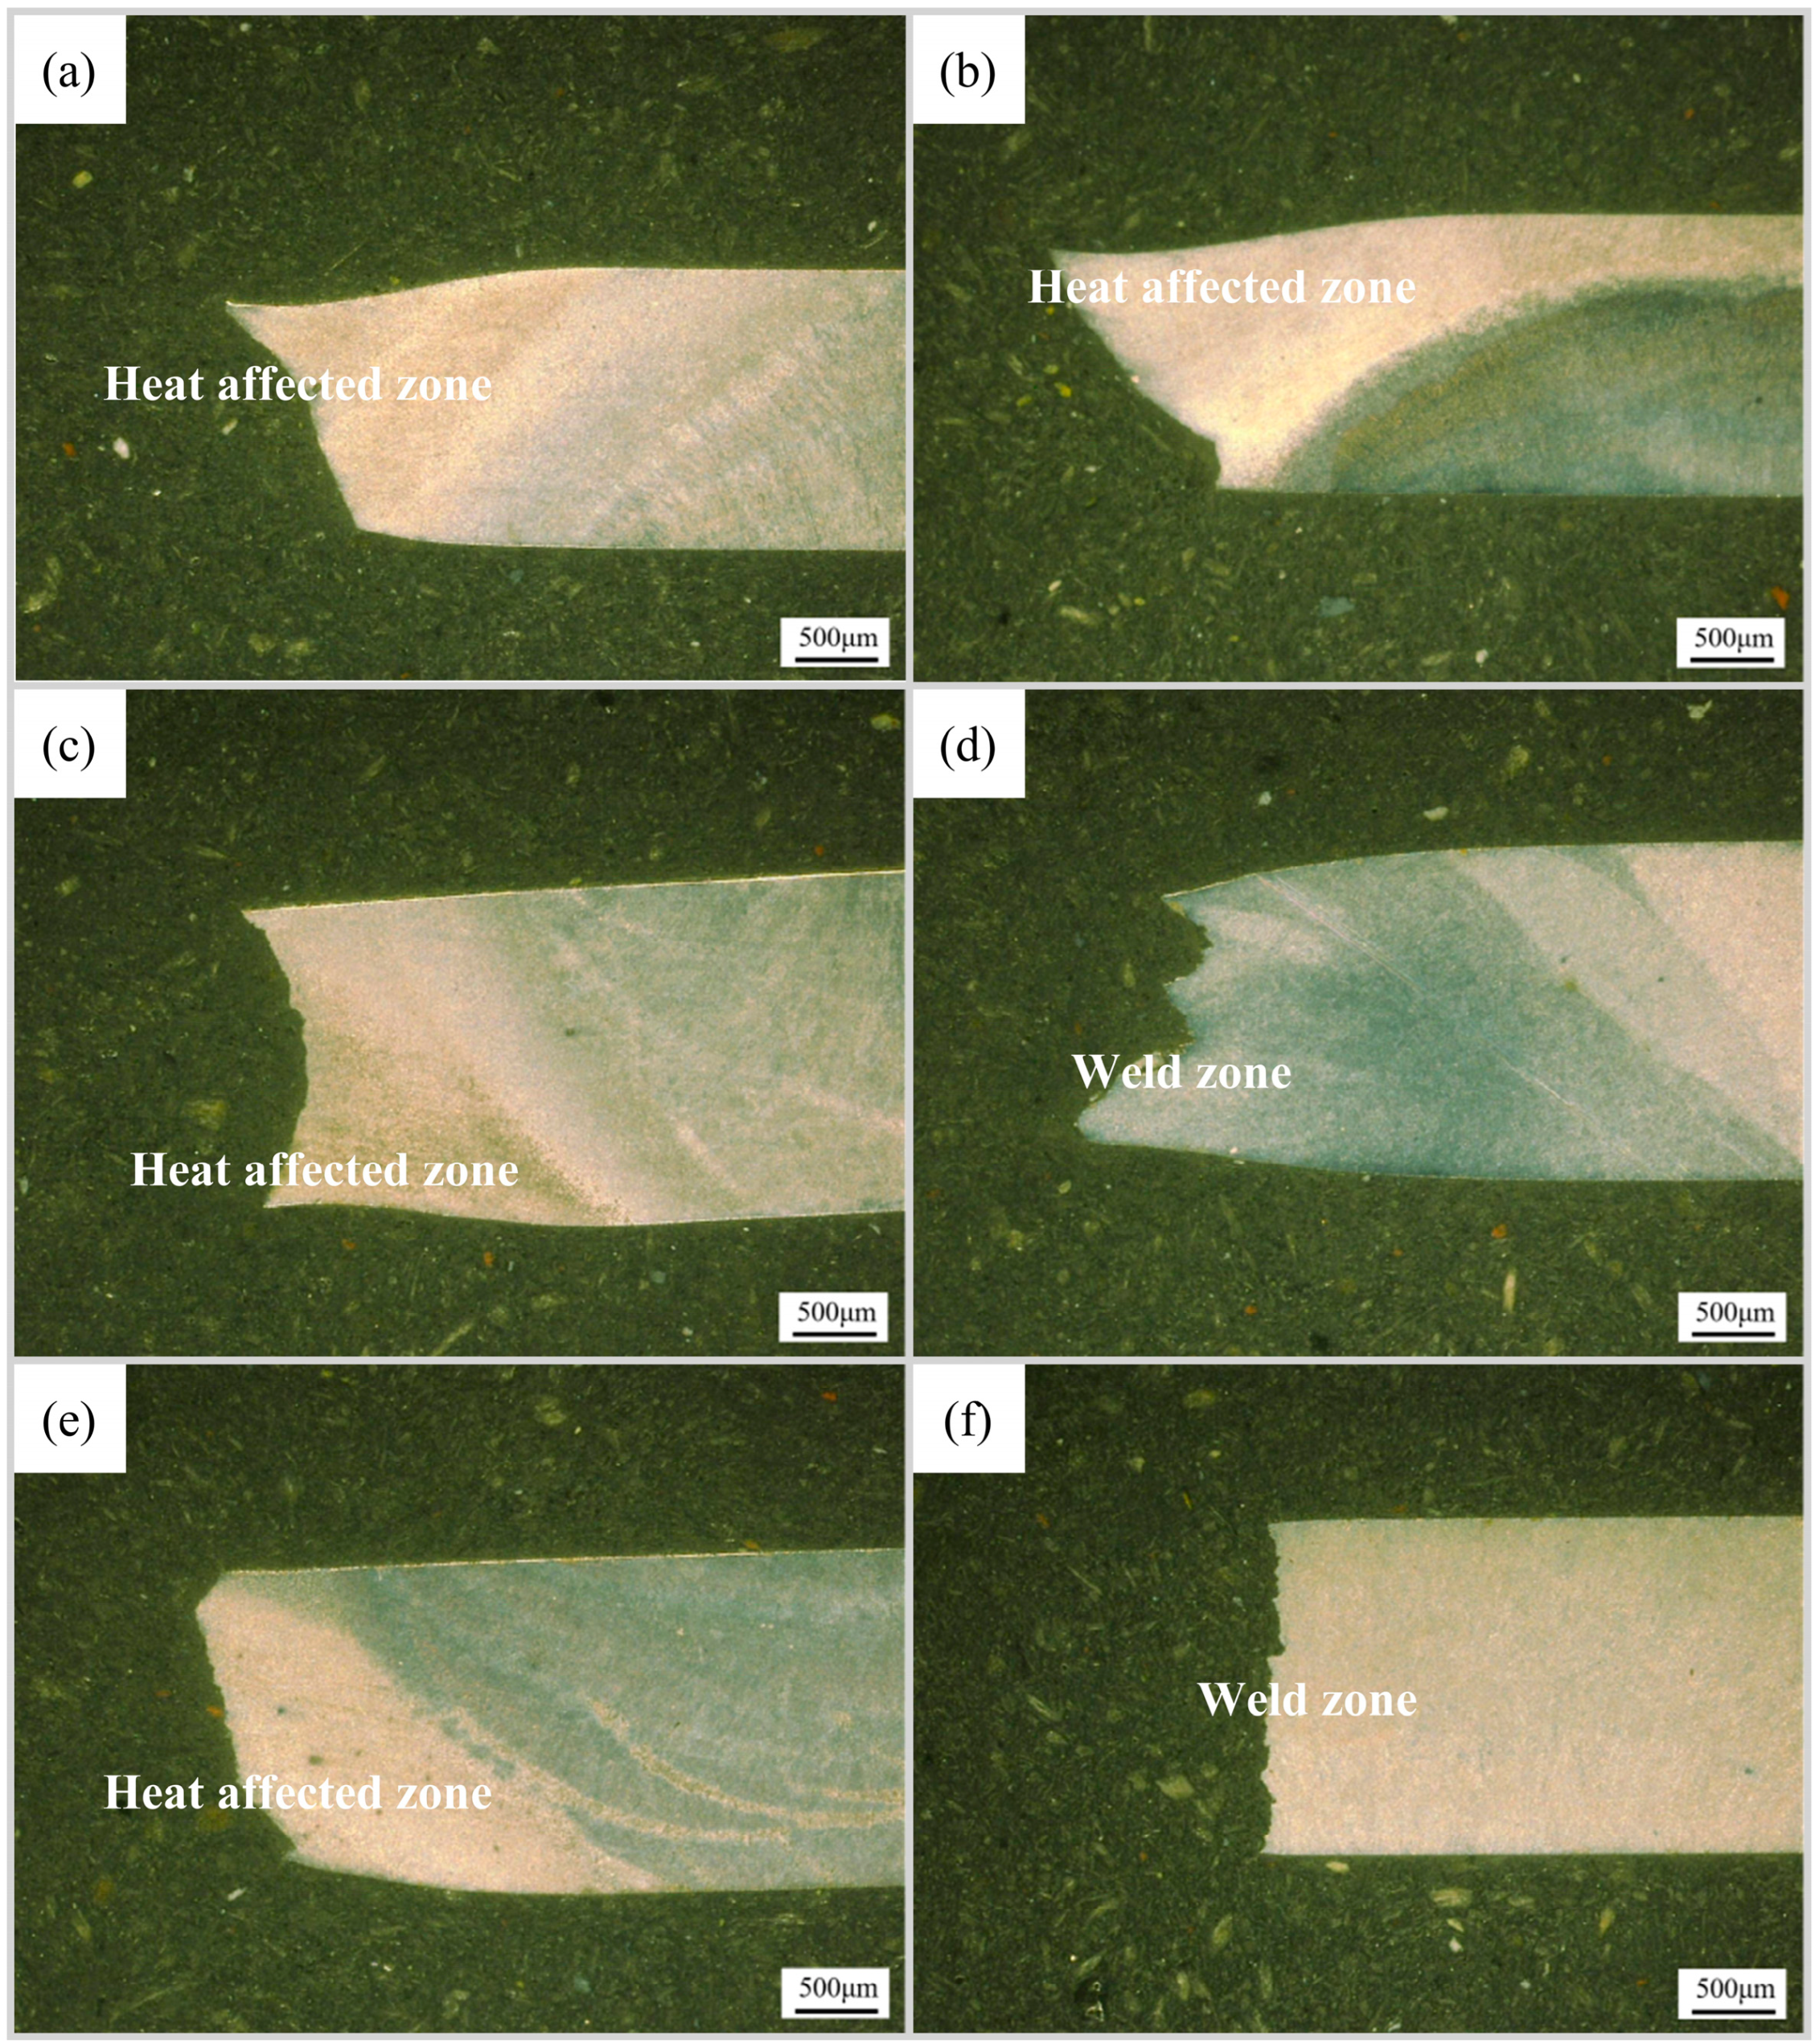
A welded joint consists of the weld zone, the HAZ, and the base metal; due to differences in the welding heat cycle, the microstructure and mechanical properties differ among these zones. Under tensile loading, there are marked differences in the fracture locations in welded joints with different tensile strengths; the fracture locations directly indicate areas of weakness in the joint’s mechanical properties. As shown in Figure 9a,c,e, all tensile specimens of the welded joints after post-weld tempering fractured within the HAZ. As shown in Figure 9b, the tensile fracture of the welded joint fabricated with HM welding wire after post-weld quenching and tempering occurred within the HAZ. In contrast, tensile fractures in welded joints fabricated with LC and BM welding wires after post-weld quenching and tempering occurred in the weld metal, as shown in Figure 9d,f. It was also observed that, after post-weld quenching and tempering, the fracture surfaces of tensile specimens from the HM- and LC-welded joints exhibited pronounced plastic deformation characteristics, whereas the fracture surface of the BM-welded joint specimen was relatively smooth, with no obvious necking. This observation is consistent with the stress–strain curves shown in Figure 8, where the BM-AQT tensile specimen fractured immediately after reaching the ultimate tensile strength.
Figure 9.
Location of tensile fracture: (a) HM-TT; (b) HM-AQT; (c) LC-TT; (d) LC-AQT; (e) BM-TT; (f) BM-AQT.
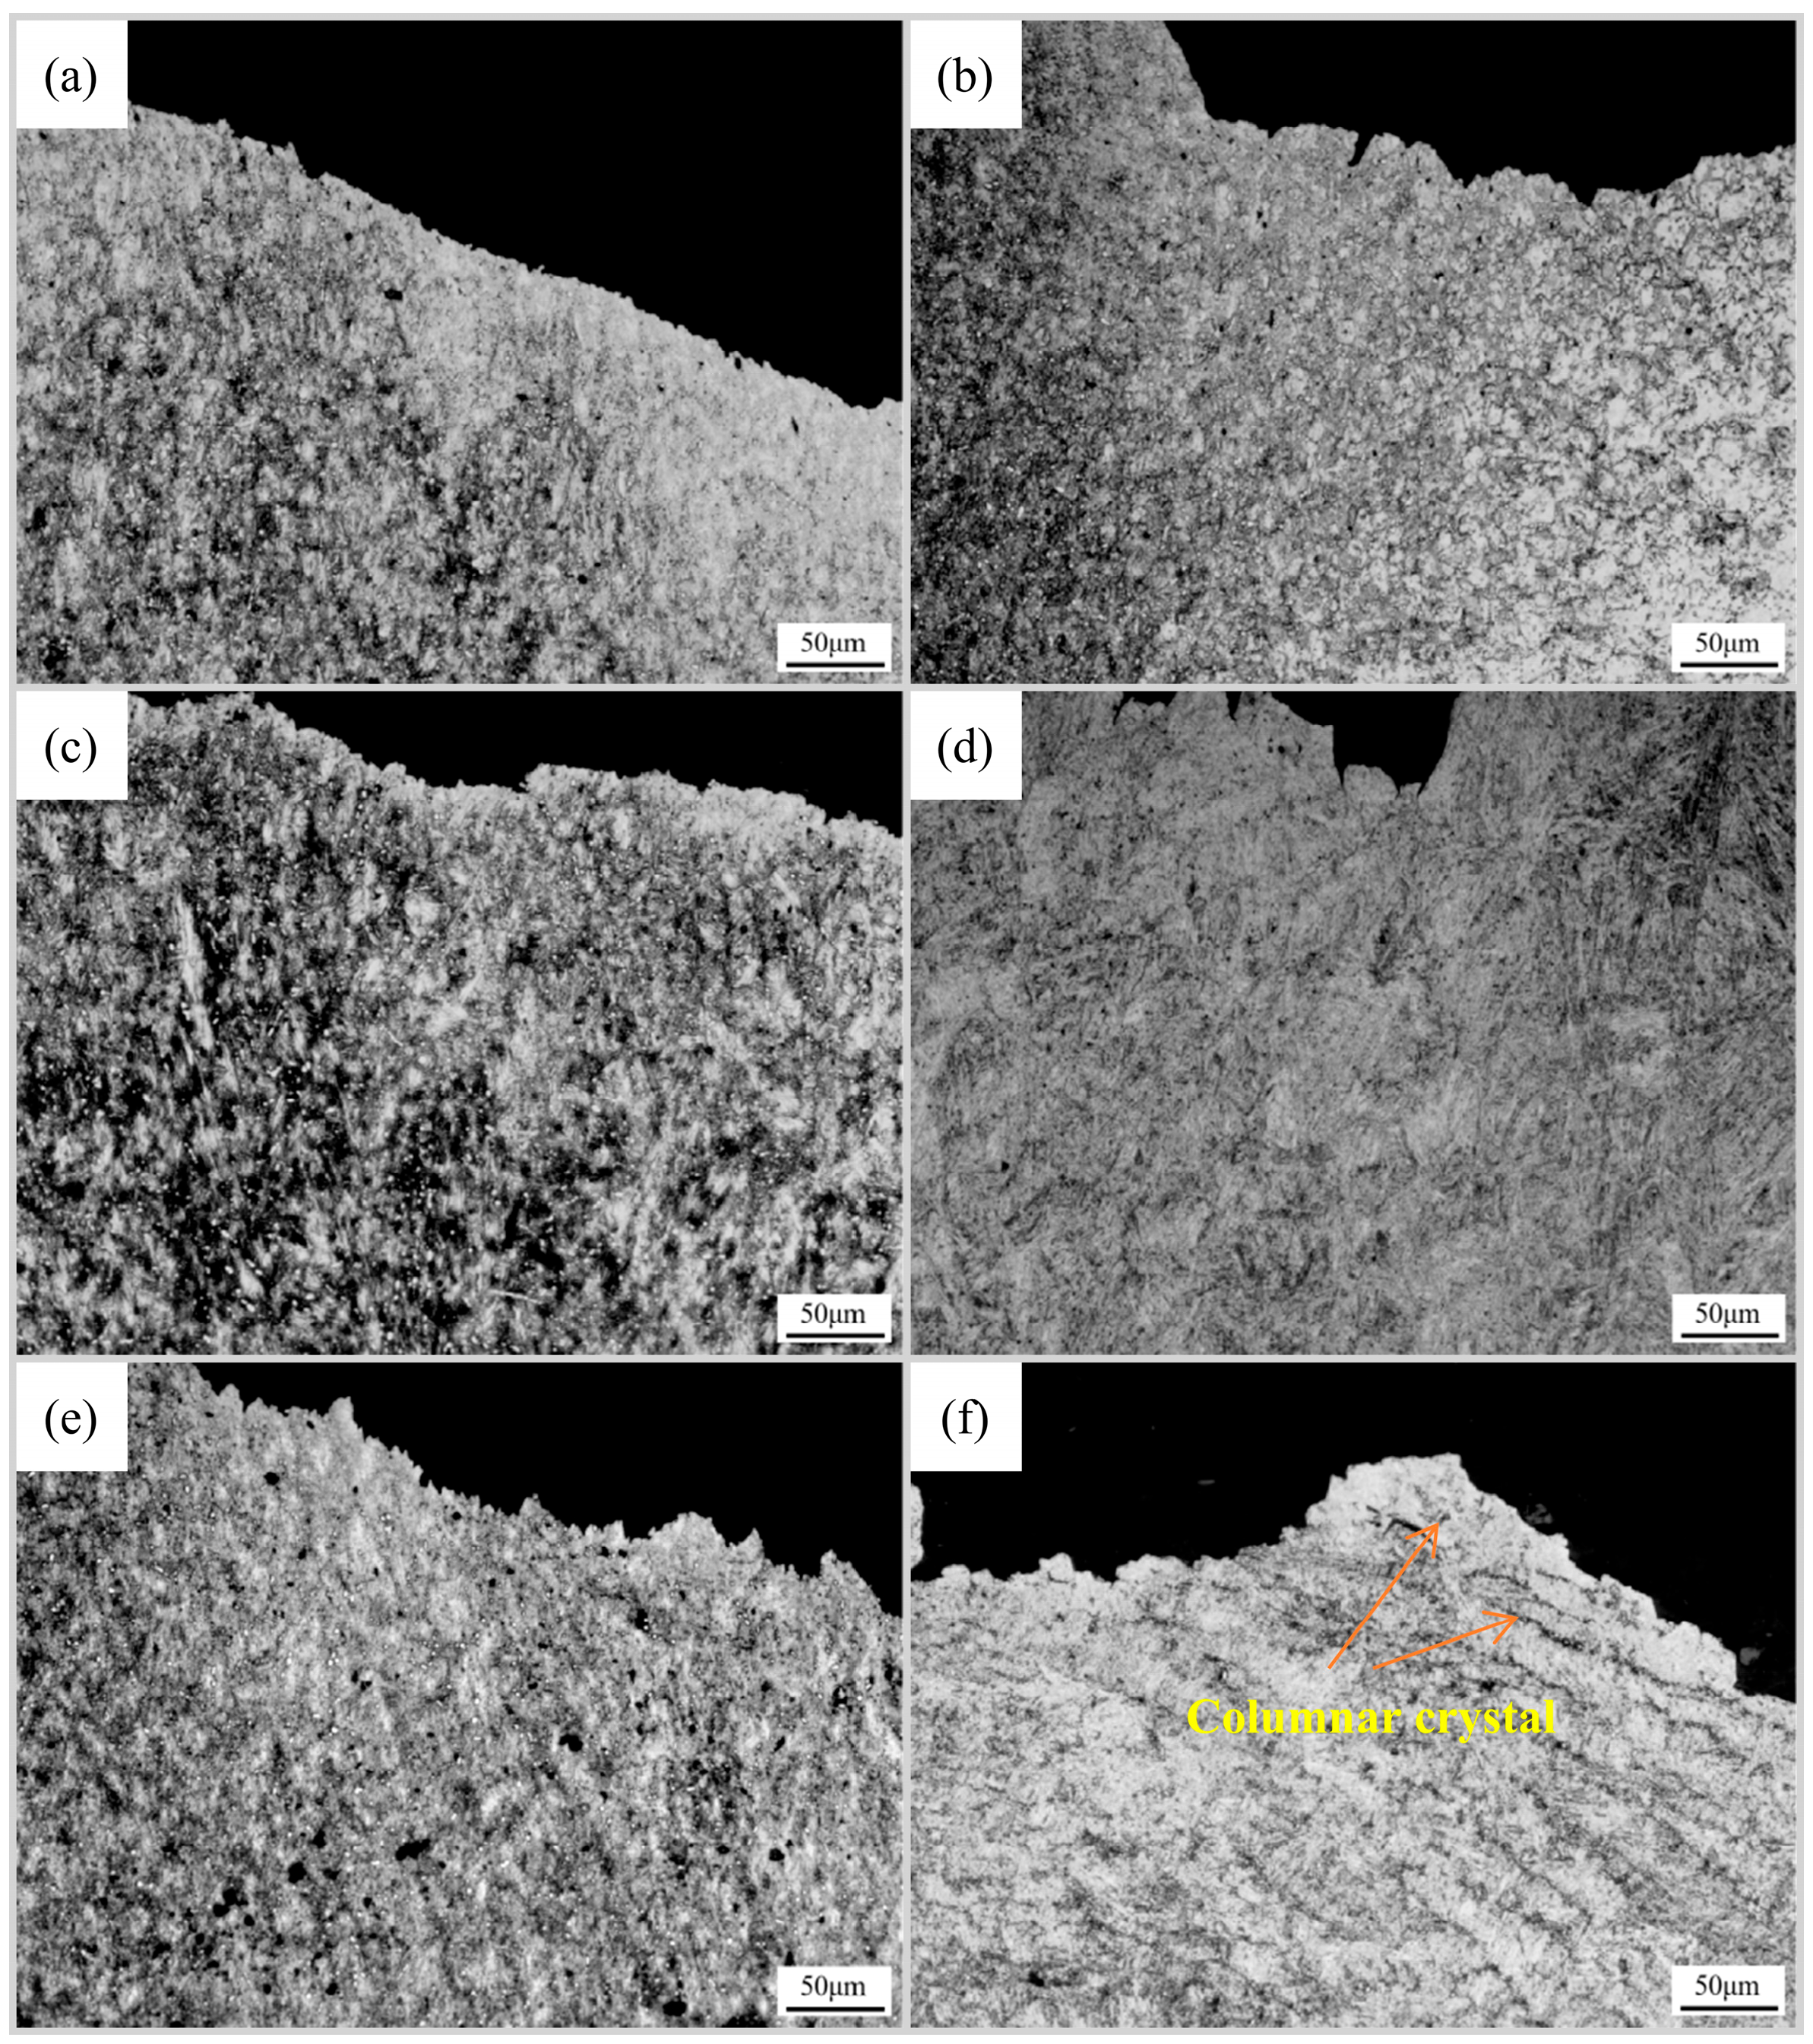
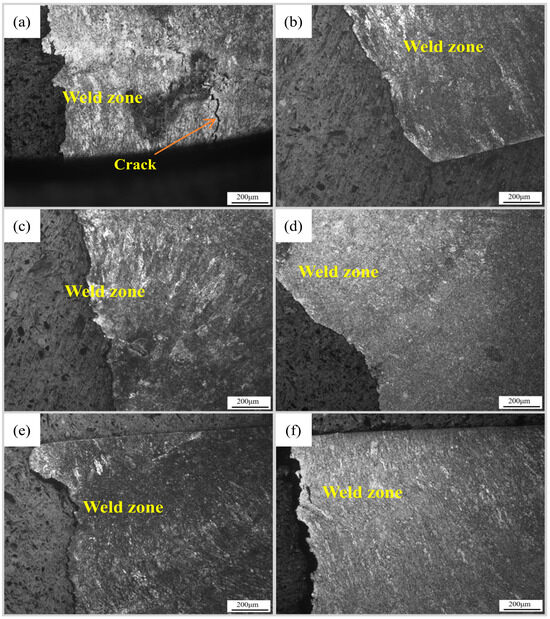
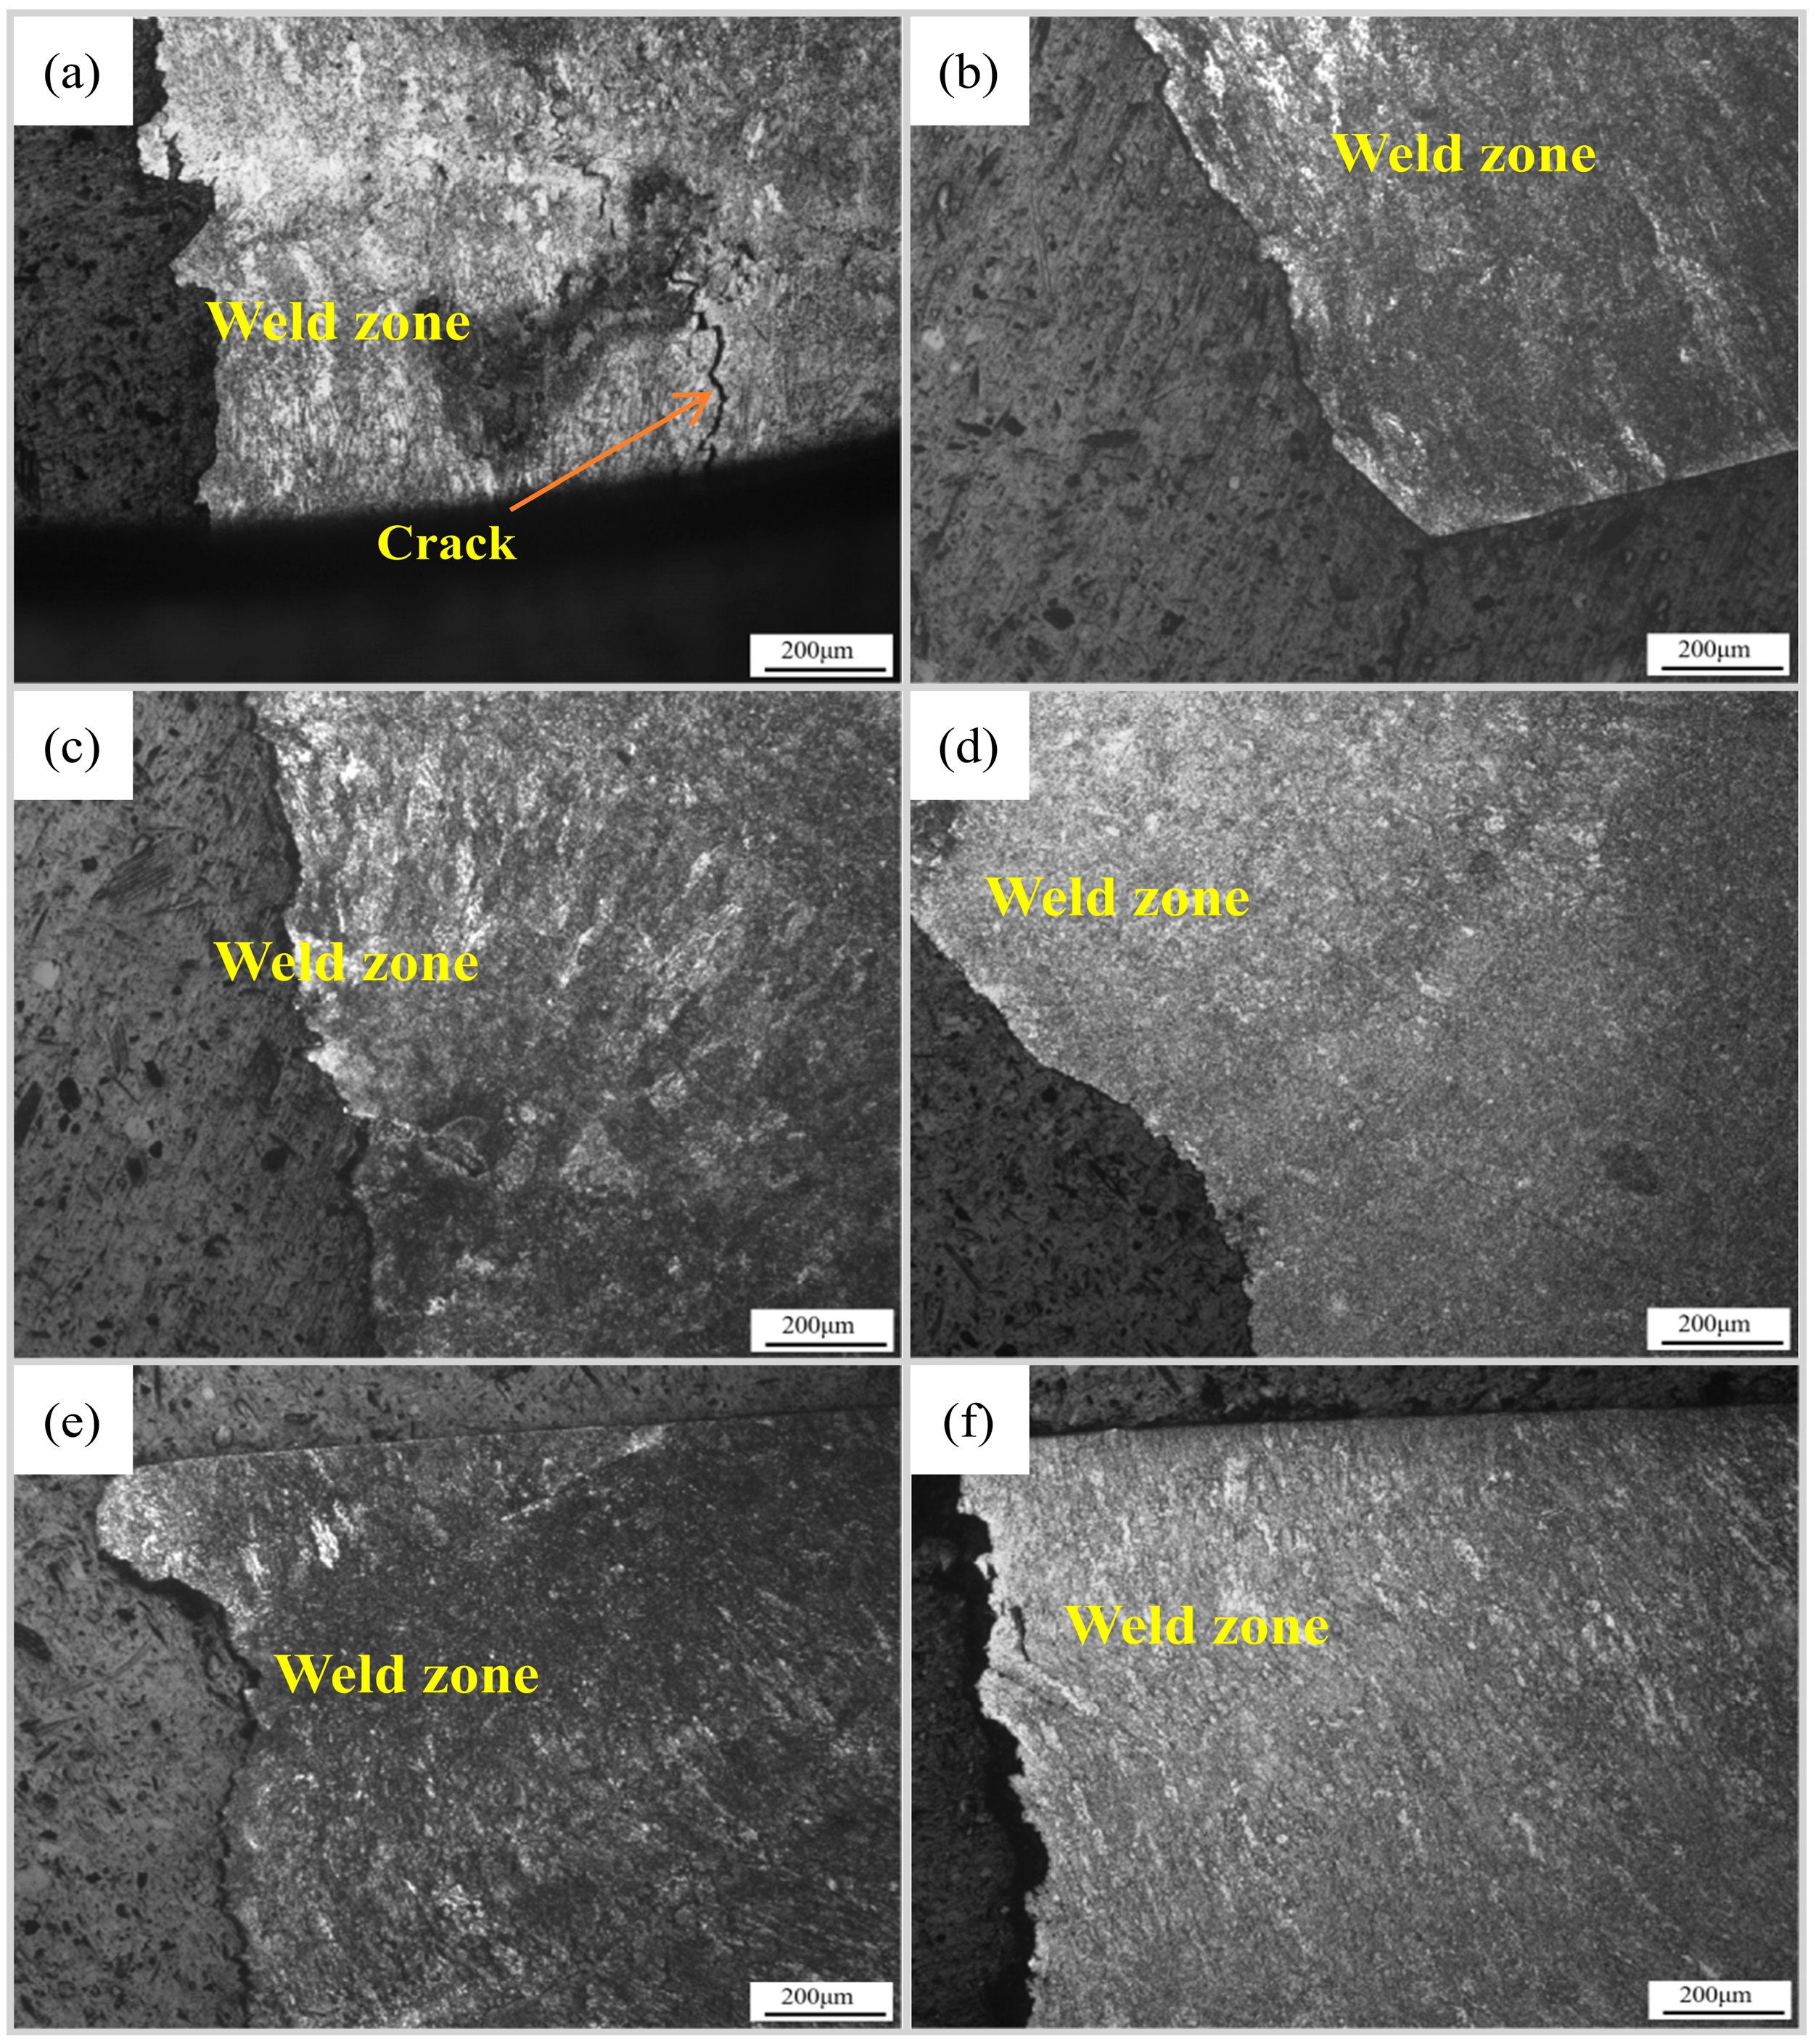
To further analyze the relationship between tensile strength and fracture location, the microstructures near the fracture surfaces of tensile specimens from different welded joints were examined using a metallographic microscope, as shown in Figure 10. Figure 10a, Figure 10c and Figure 10e show the microstructures near the tensile fracture surfaces of specimens fabricated with HM, LC and BM welding wires after post-weld tempering, respectively. The microstructures near the fracture surfaces are relatively coarse, with numerous second-phase particles distributed throughout the observed regions. As can be seen from Figure 10b, the microstructure near the fracture surface of the tensile specimen from the HM-welded joint after post-weld quenching and tempering consists of tempered martensite and undissolved carbides.
Figure 10.
Metallographic structure near tensile fracture: (a) HM-TT; (b) HM-AQT; (c) LC-TT; (d) LC-AQT; (e) BM-TT; (f) BM-AQT.
As can be seen from Figure 9b, the specimen fractured in the HAZ adjacent to the weld, indicating that the weld metal has higher strength than the HAZ. Since the HAZ is the weakest region of the welded joint, the specimen fractured preferentially in this region under tensile loading. As can be seen from Figure 9d, the fracture microstructure of the LC welding wire tensile test specimens after quenching and tempering is tempered martensite, with distinct lamellar features. Figure 10f shows the microstructure near the fracture surface of a tensile specimen from the BM welded joint after post-weld quenching and tempering. It can be seen that the microstructure of the weld metal is non-uniform, with the original columnar dendritic morphology still present; the fracture path is consistent with the dendrite growth direction in the weld metal.
As can be seen from Figure 11a,b, the tensile fracture surfaces of specimens from the HM welded joint after post-weld tempering exhibit a mixture of ductile and brittle fracture characteristics. The fracture surfaces are uneven, with a large number of ductile dimples distributed across them; these dimples are surrounded by distinct tear ridges, and some small cleavage planes are also present. As can be seen from Figure 11c,d, the tensile fracture surface of the specimen from the HM welded joint after post-weld quenching and tempering is generally smooth, with a large number of irregularly sized ductile dimples distributed across the surface; at the same time, a small number of cleavage planes and river-like patterns are visible. The fracture mode is predominantly ductile, accompanied by localized quasi-cleavage fracture characteristics.
Figure 11.
SEM morphology of tensile fracture of HM welding wire welded joint: (a,b) HM-TT; (c,d) HM-AQT.
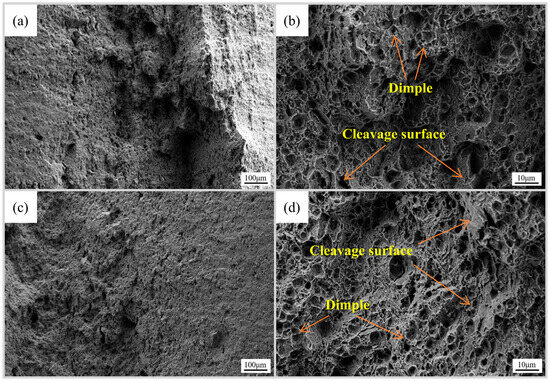
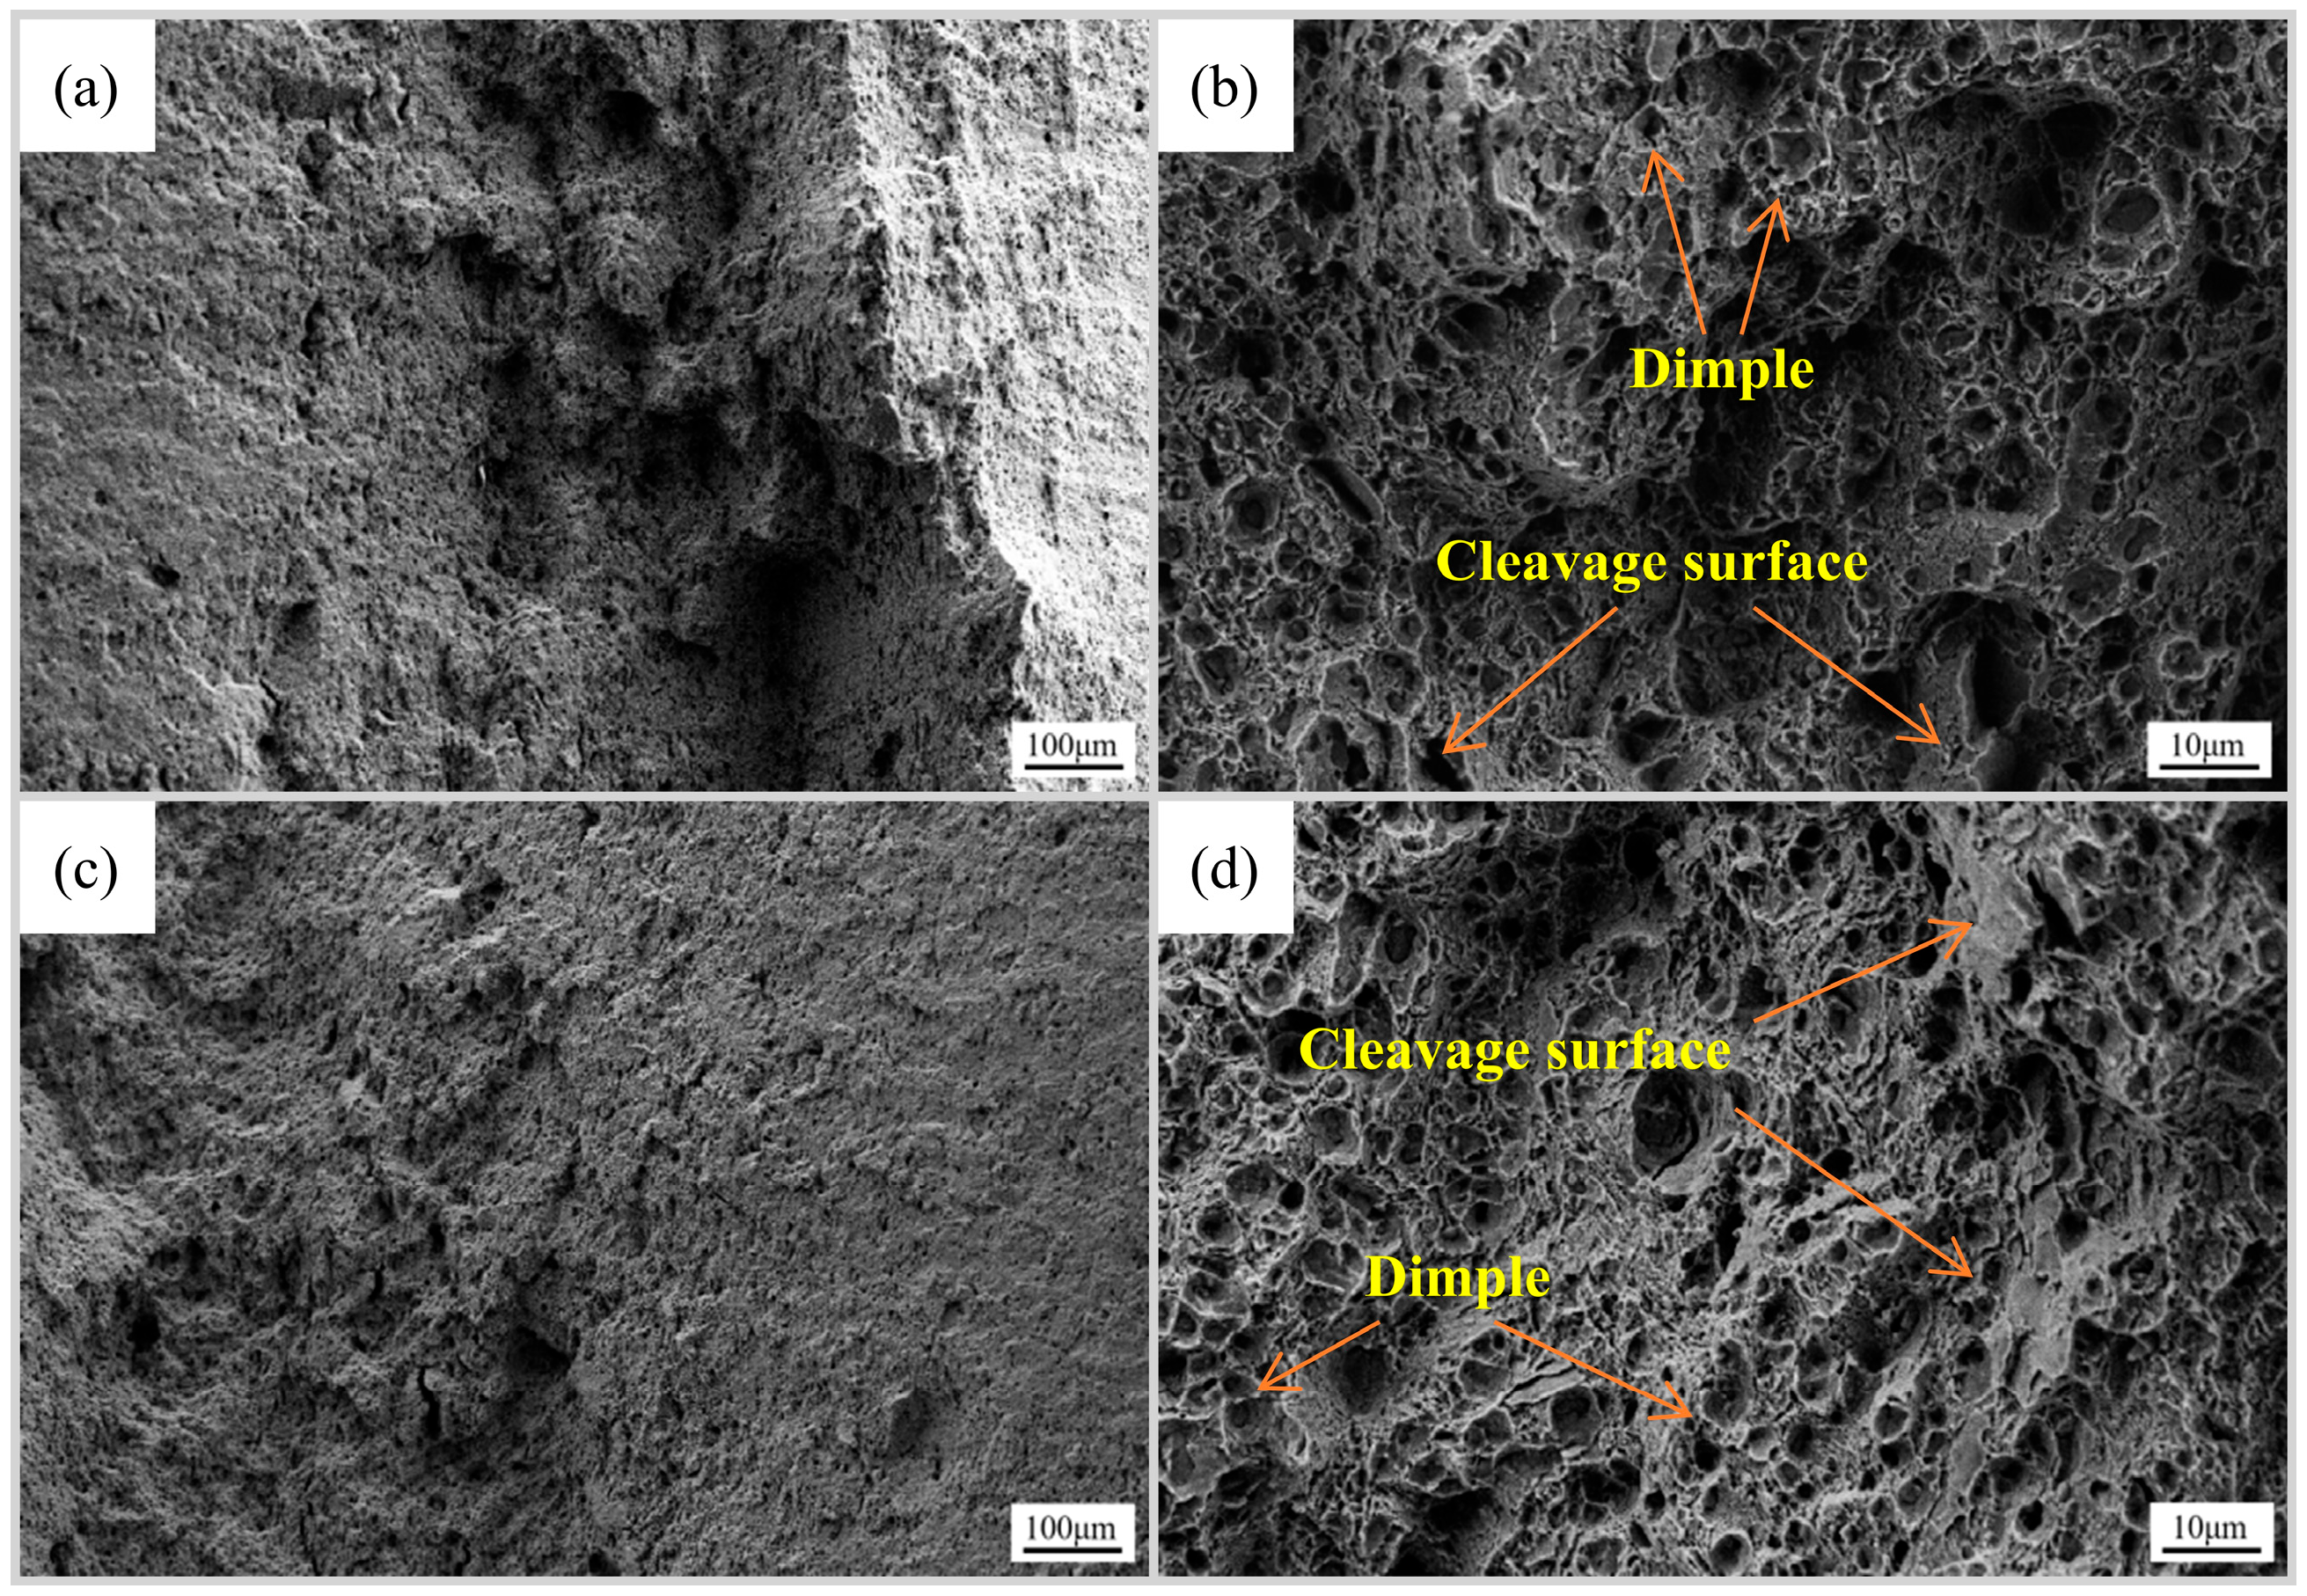
As can be seen from Figure 12a,b, the tensile fracture surfaces of specimens from the LC welded joint after post-weld tempering exhibit numerous cleavage planes and some small ductile dimples, with distinct tear ridges and river-like patterns, indicating quasi-cleavage fracture. Figure 12c,d shows the fracture surfaces of tensile specimens from the LC welded joint after post-weld quenching and tempering. A number of protrusions can be observed on the fracture surfaces, indicating clear signs of plastic deformation. The fracture surfaces are covered with a large number of fine ductile dimples, while small cleavage steps and river-like patterns are present in some areas of the fracture surfaces. Overall, the fracture exhibits characteristics of a mixed fracture consisting of ductile fracture and quasi-cleavage fracture.
Figure 12.
SEM morphology of tensile fracture of LC welding wire welded joint: (a,b) LC-TT; (c,d) LC-AQT.
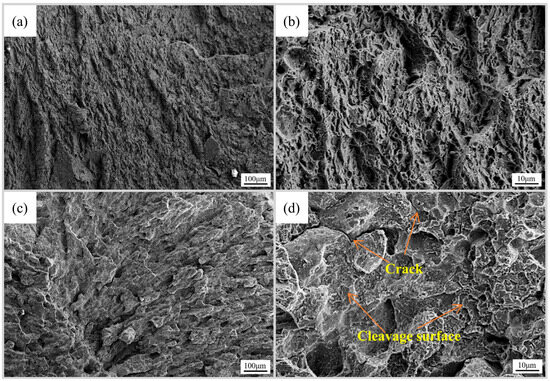
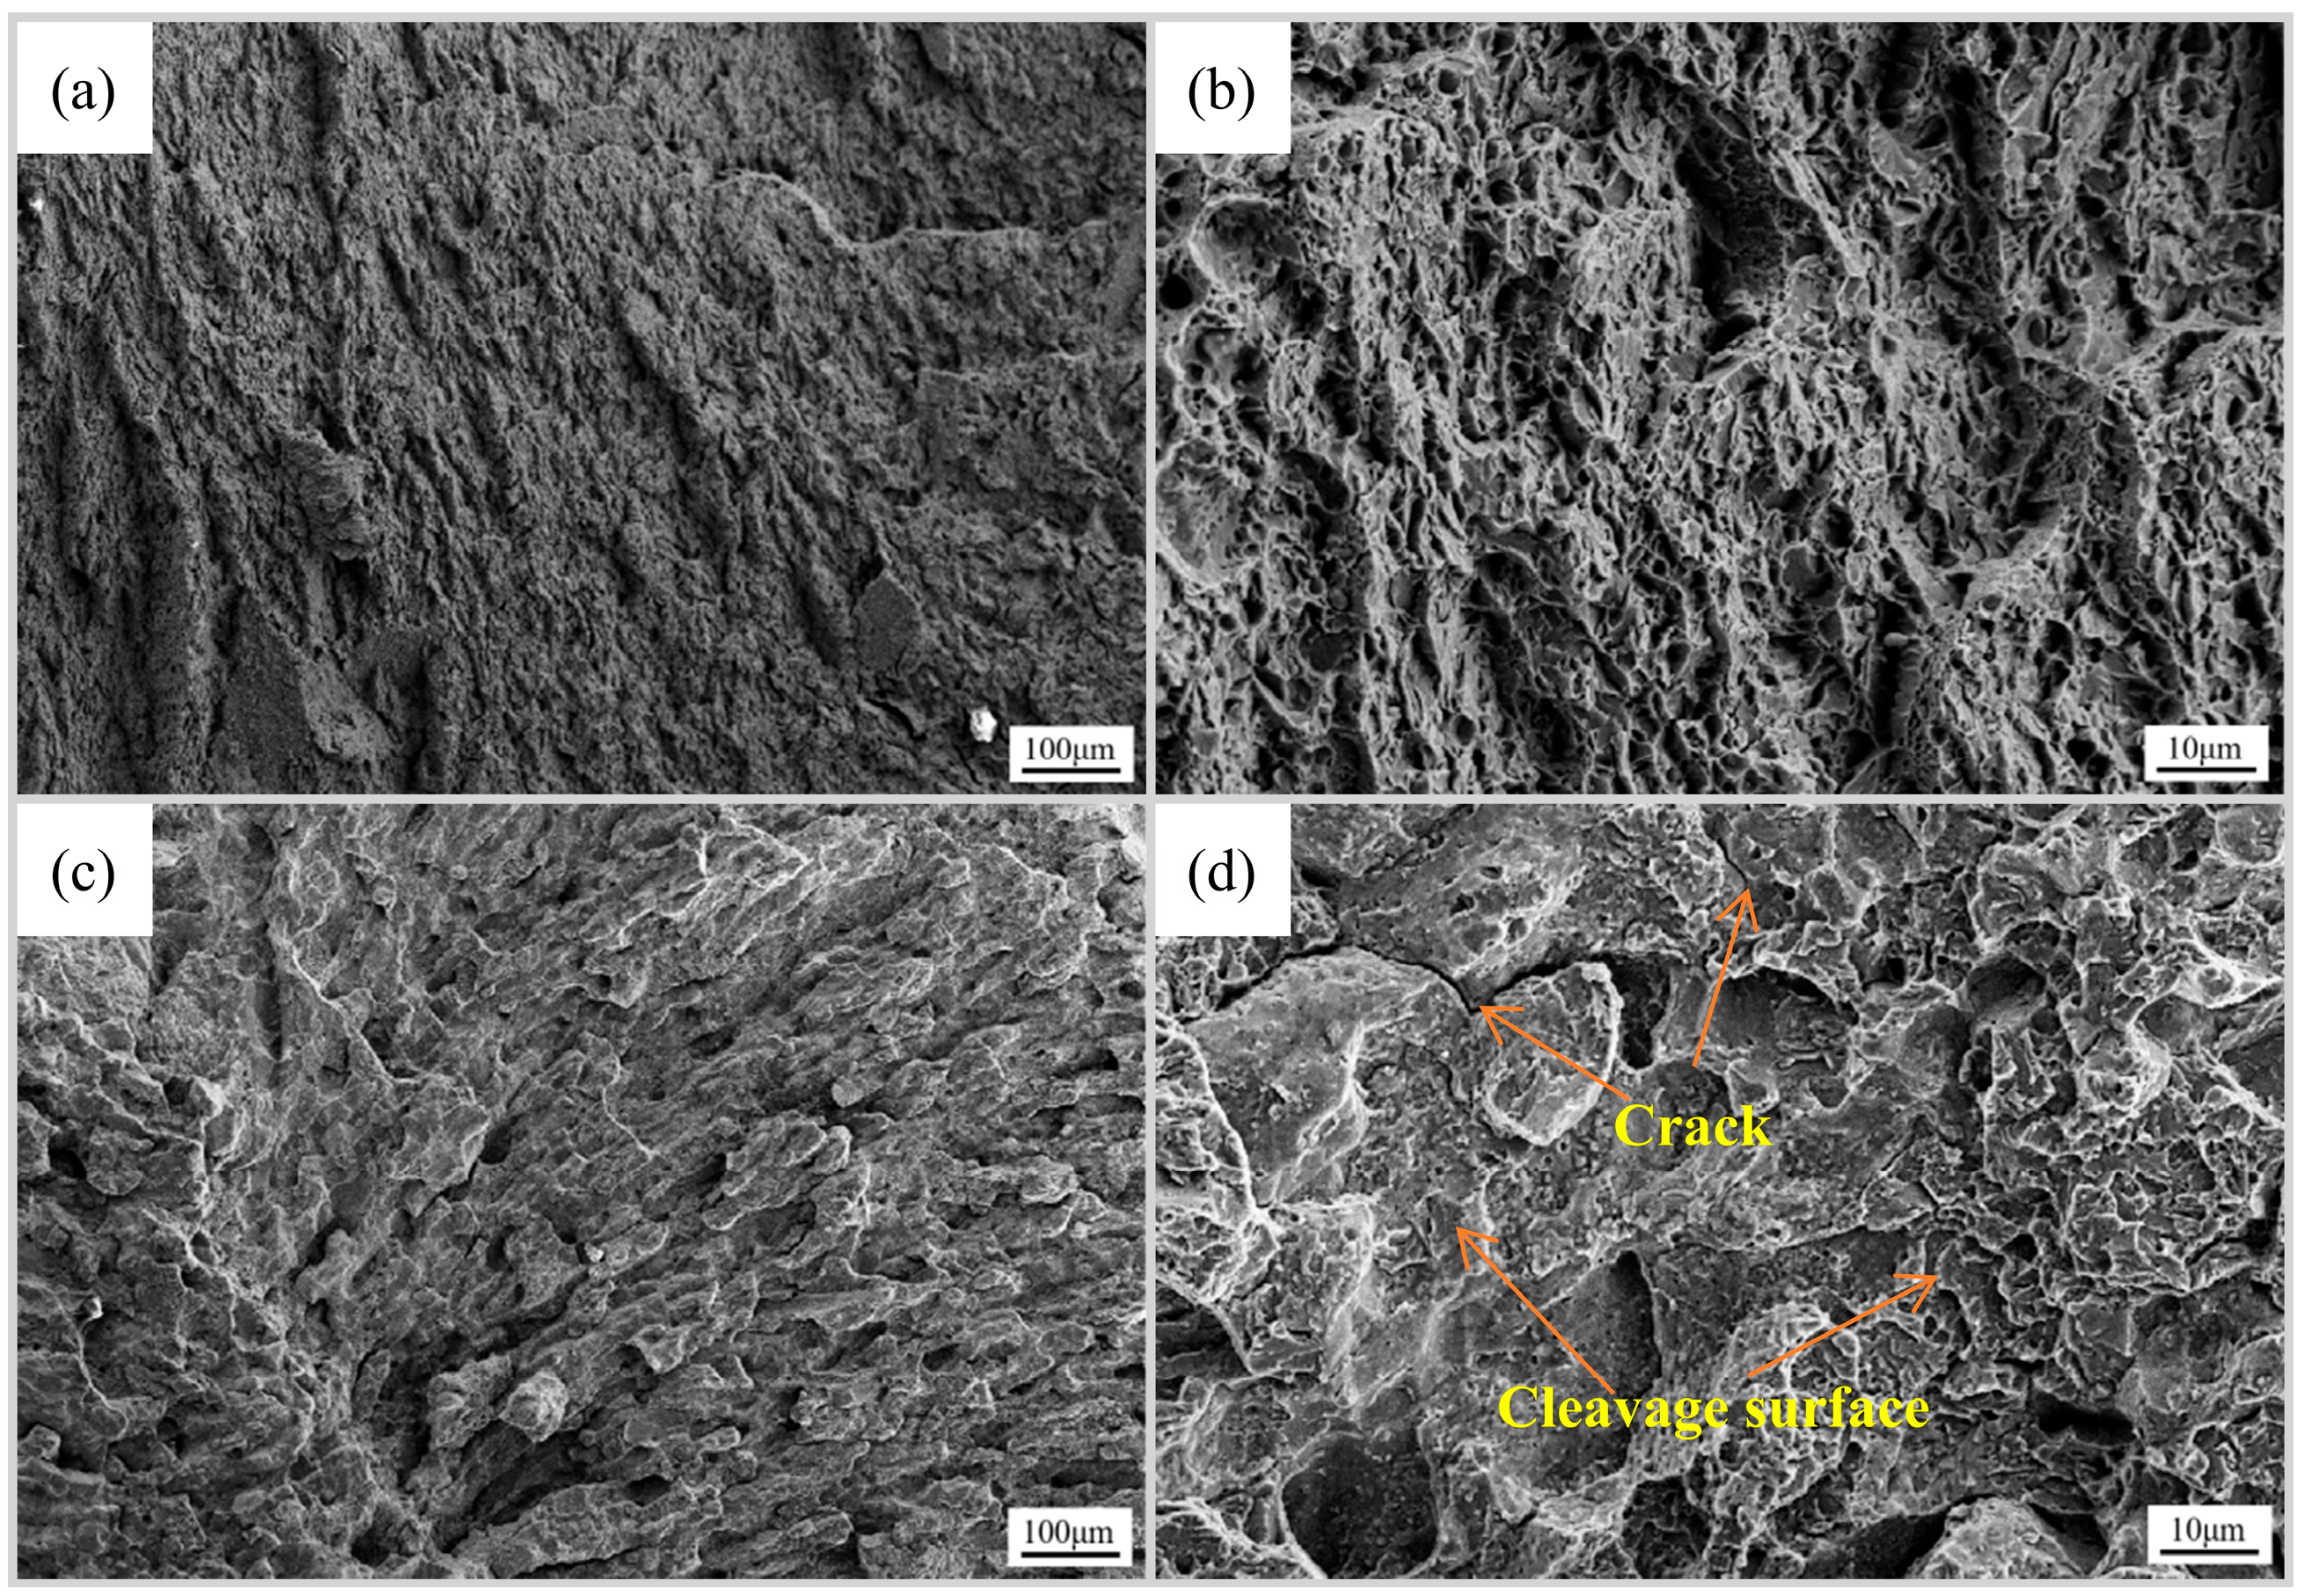
Figure 13a,b shows the tensile fracture surface morphology of specimens fabricated with BM welding wire after post-weld tempering. Distinct tear ridges and cleavage steps were observed, along with some small dimples, indicating quasi-cleavage fracture characteristics. Figure 13c,d shows the tensile fracture surface morphology of specimens from the BM welded joint after post-weld quenching and tempering. It can be seen that the fracture surface is generally smooth, with distinct directional features on the fracture surface, revealing the columnar grain morphology of the weld metal. Distinct cleavage planes and intergranular cracks were observed, indicating mixed brittle fracture behavior characterized by intergranular fracture and quasi-cleavage fracture.
Figure 13.
SEM morphology of tensile fracture of BM welding wire welded joint: (a,b) BM-TT; (c,d) BM-AQT.
3.3. Impact Toughness
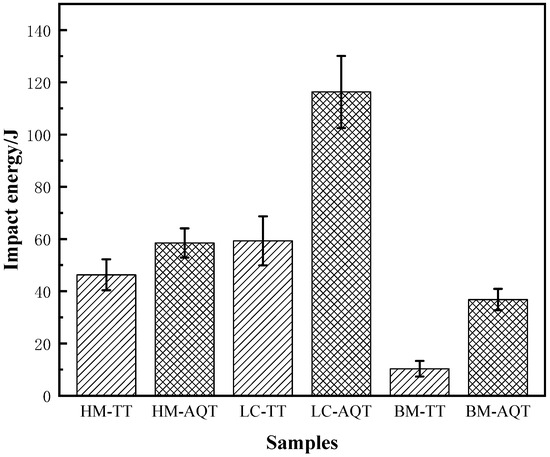
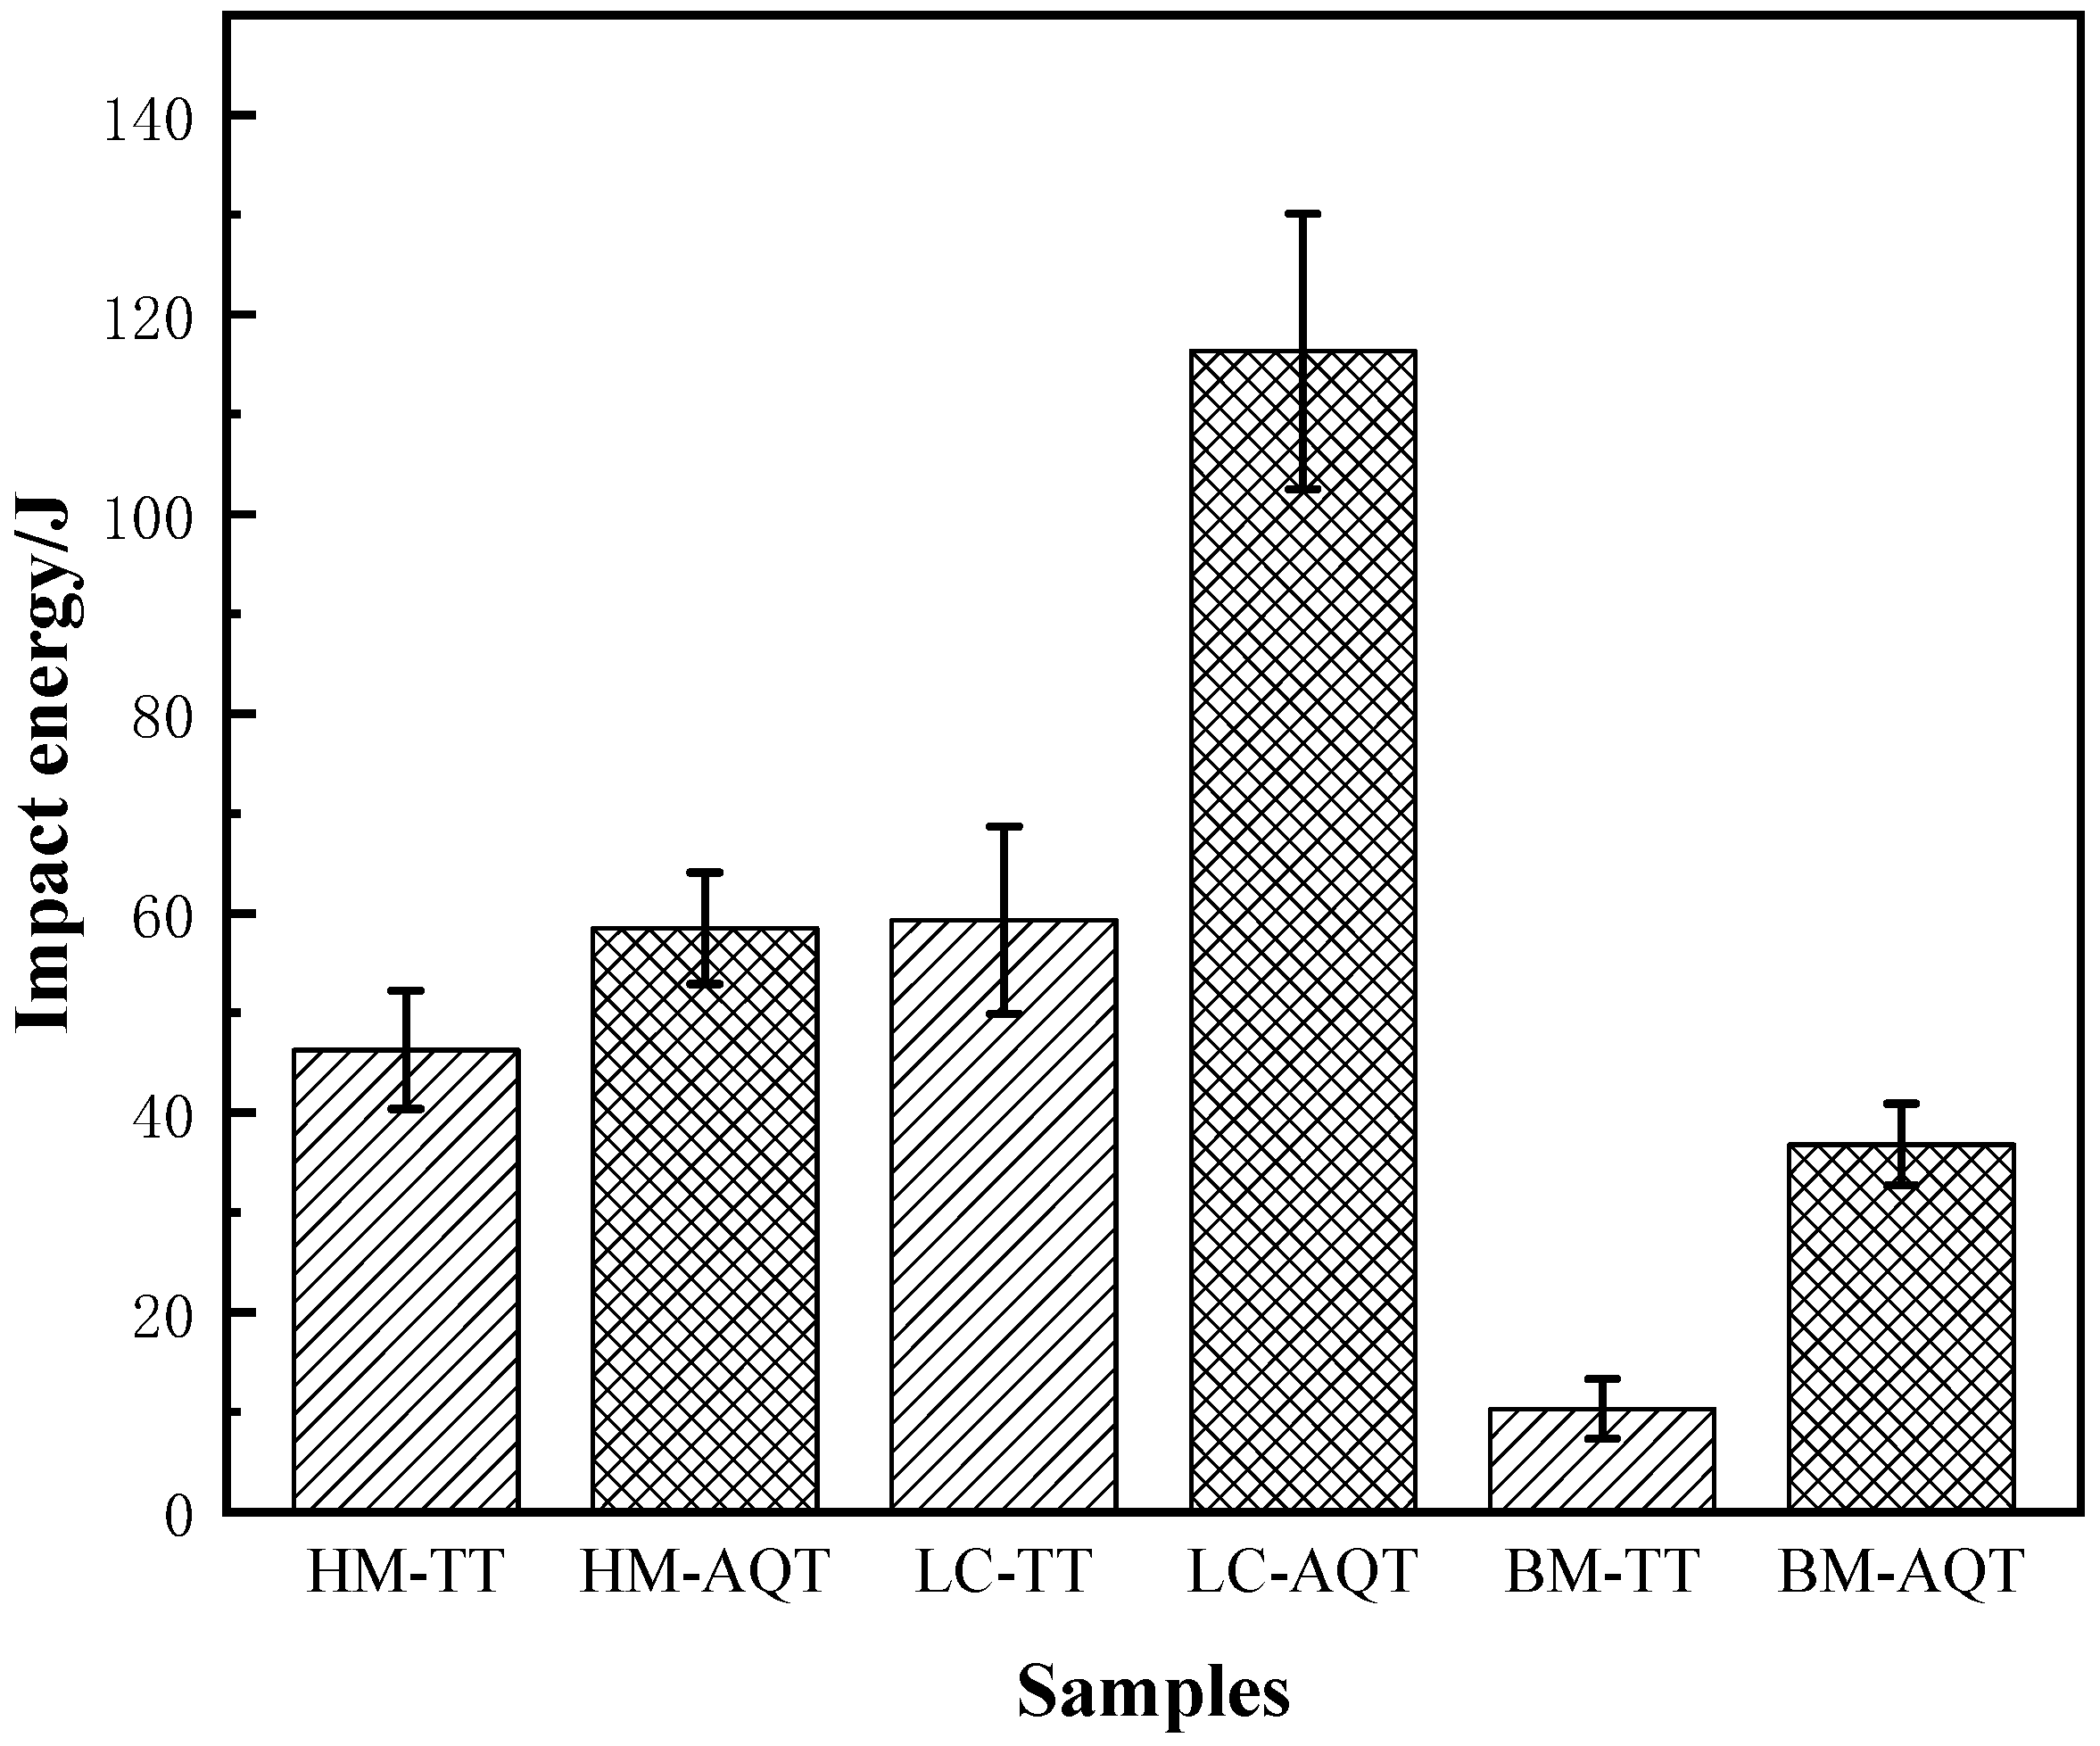
As shown in Figure 14, the impact energies of welded joints produced using HM, LC, and BM welding wires after post-weld tempering were 46.3 J, 59.3 J, and 10.3 J, respectively, whilst those after post-weld quenching and tempering were 58.9 J, 116.3 J, and 36.8 J, respectively. The impact energy data in Figure 14 are presented as mean value ± SD, calculated from independent specimens. Under the same post-weld heat treatment process, the impact energy values of welded joints produced using all three types of welding wire follow the pattern LC > HM > BM; for a given type of welding wire, impact energy after post-weld quenching and tempering is higher than that after post-weld tempering. Among the tested welded joints, the LC welded joint after post-weld quenching and tempering exhibited the highest impact energy (116.3 J), although it remained lower than that of the base material under the same heat-treatment condition (220.7 J).
Figure 14.
Impact test results of welded joints.
All impact test specimens fractured in the weld metal, and the microstructure near the fracture surface is shown in Figure 15. Except for the post-weld quenched and tempered specimen from the LC welded joint (Figure 15d), the fracture surfaces of the other impact test specimens were relatively smooth; the fracture path was consistent with the columnar grain growth direction in the weld metal, and the fractures exhibited clear signs of brittle fracture. Secondary cracks were observed in the weld metal of the impact fracture surface of the specimen from the HM welded joint after post-weld tempering, as shown in Figure 15a. The crack appeared to propagate preferentially along grain boundaries. This morphology is consistent with an intergranular fracture contribution and may be associated with the relatively low impact energy measured for this condition.
Figure 15.
Metallographic structure near impact fracture: (a) HM-TT; (b) HM-AQT; (c) LC-TT; (d) LC-AQT; (e) BM-TT; (f) BM-AQT.
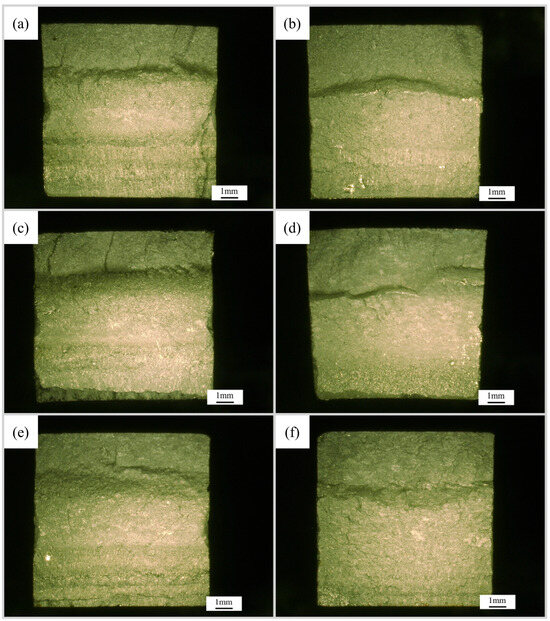
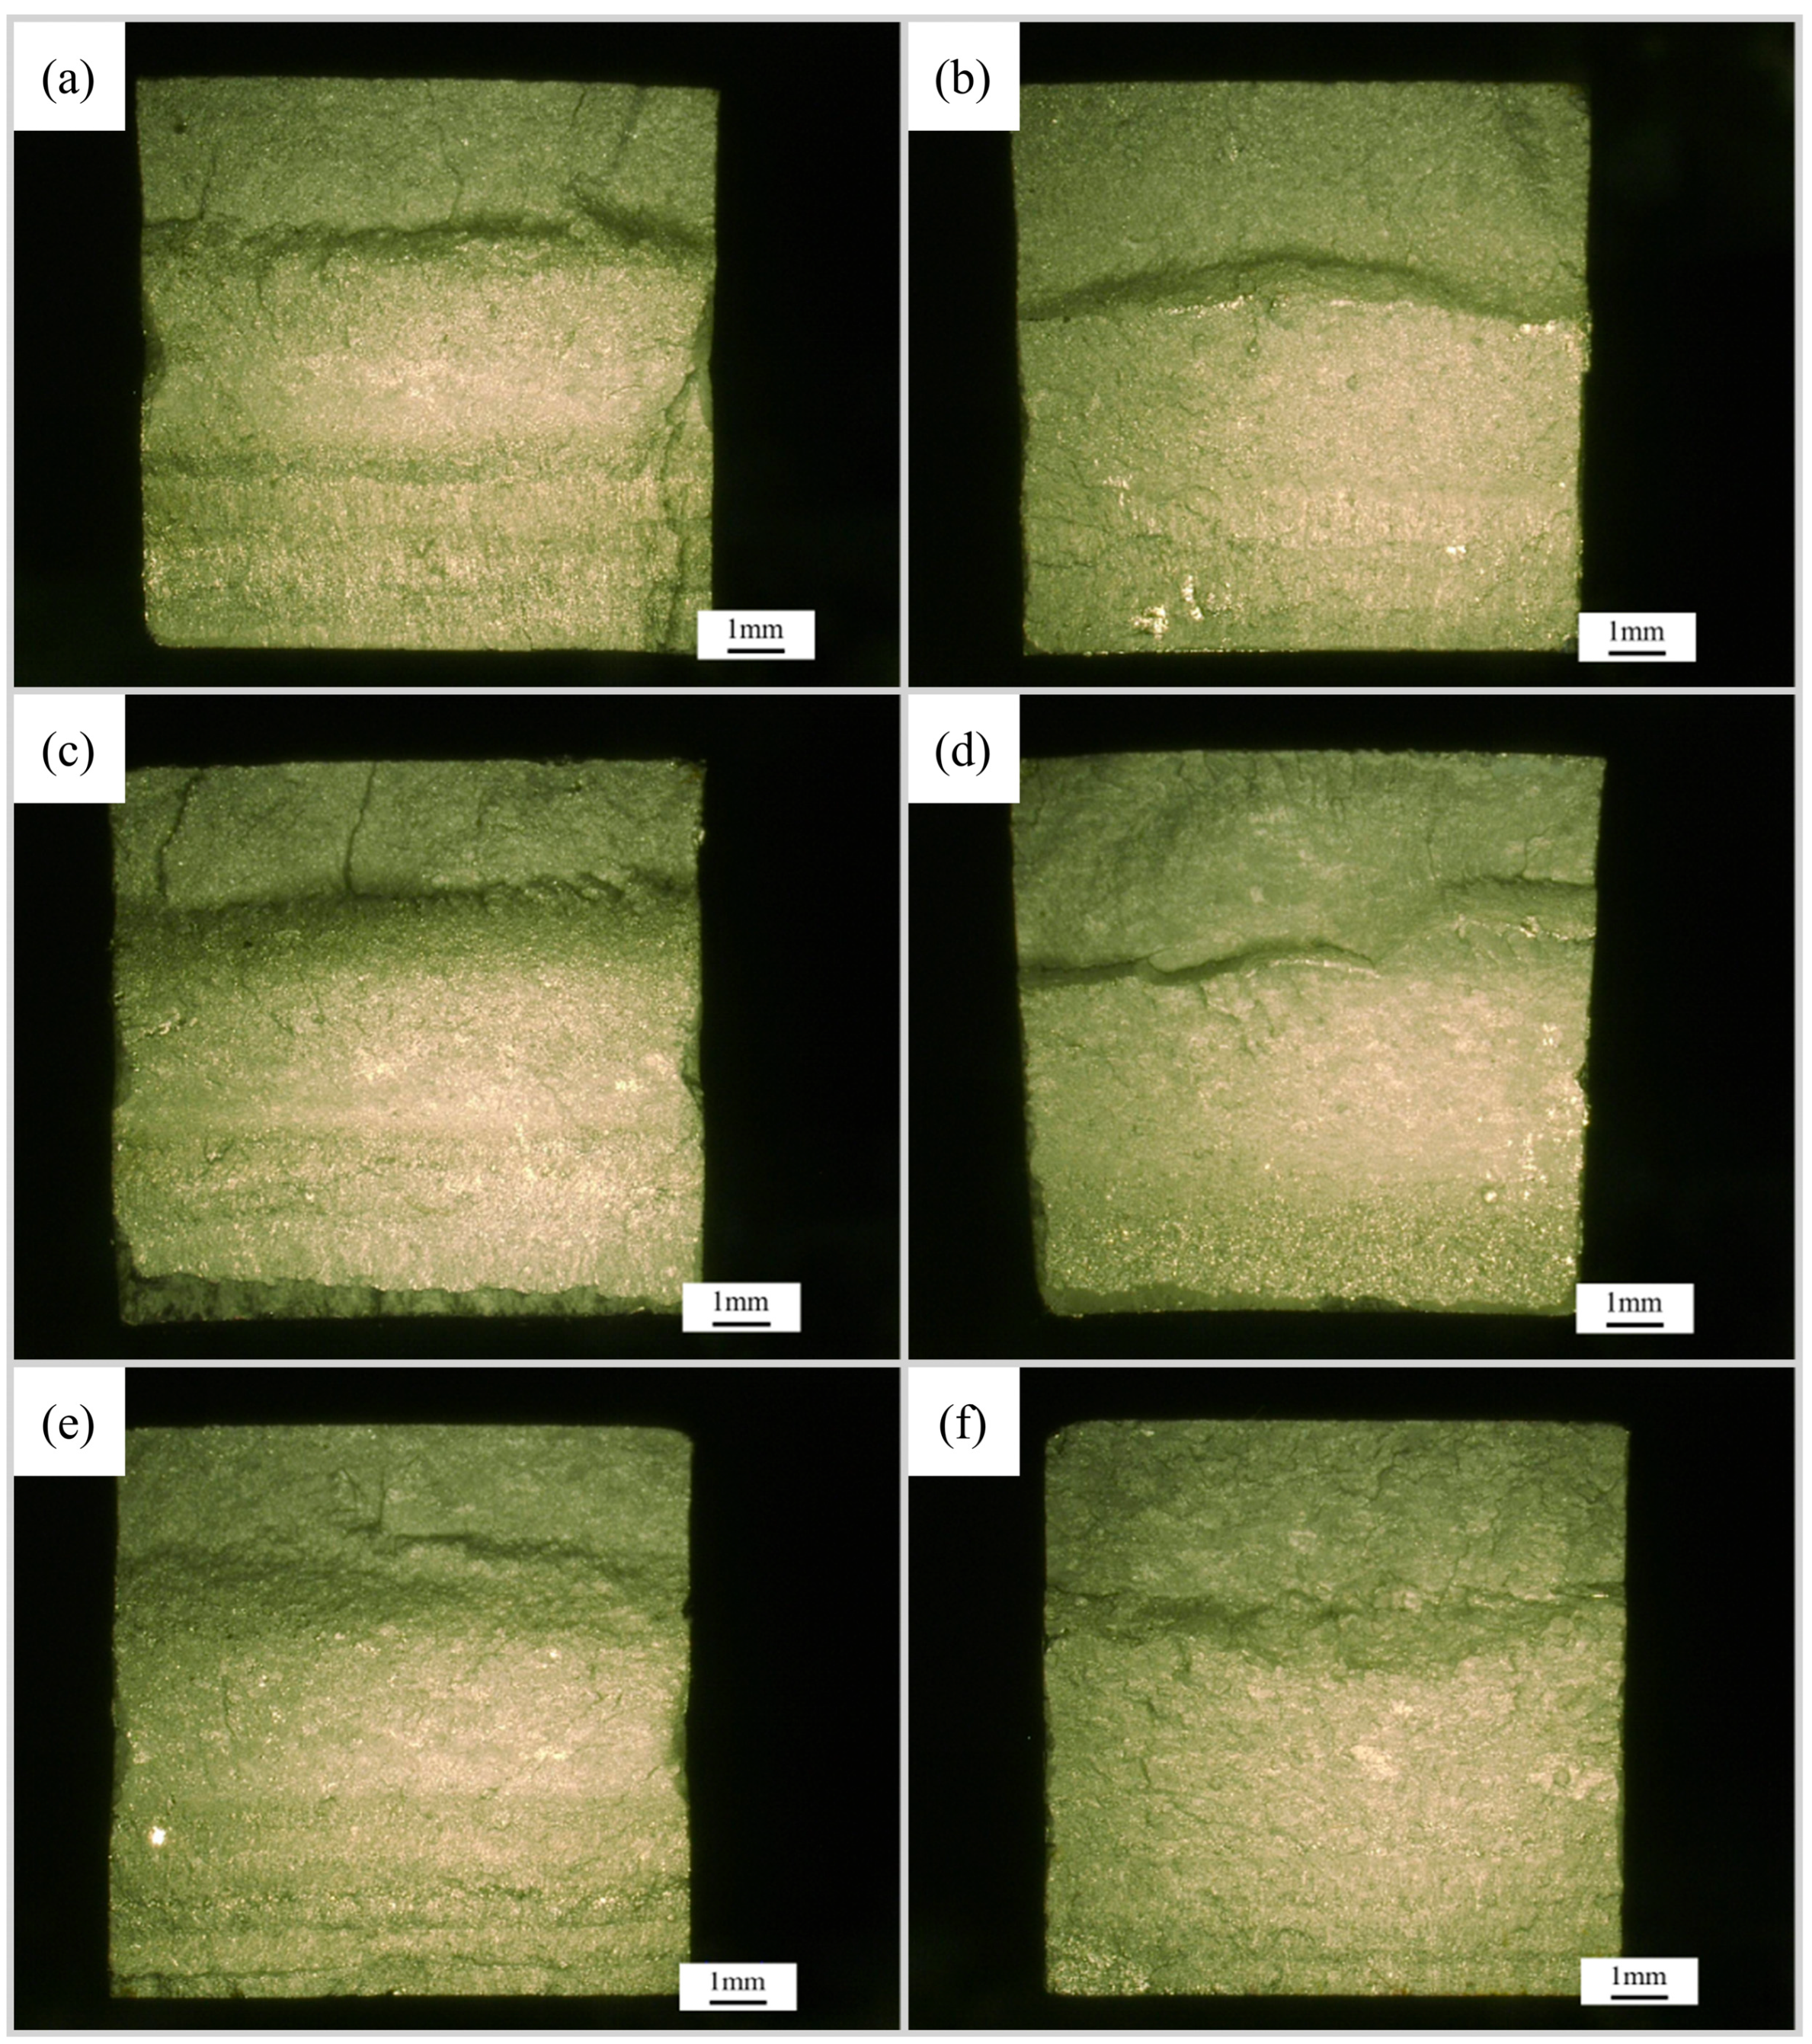
Figure 16 shows the macroscopic morphology of the impact fracture surface of a welded joint observed. It can be seen that steps are present on all fracture surfaces, and the fracture surfaces are relatively flat. Differences in fracture morphology between the weld metal and the base material are evident; the weld metal exhibits a layered pattern, indicating differences in the microstructures of different weld layers resulting from multi-layer, multi-pass welding. The impact fracture surface of the specimen from the LC welded joint after post-weld quenching and tempering (Figure 16d) exhibited a certain degree of plastic deformation, demonstrating relatively good impact toughness. The impact fracture surfaces of the remaining impact test specimens all exhibited clear signs of brittle fracture, which are consistent with the impact energy results shown in Figure 14.
Figure 16.
Macromorphology of impact fracture of welded joint: (a) HM-TT; (b) HM-AQT; (c) LC-TT; (d) LC-AQT; (e) BM-TT; (f) BM-AQT.
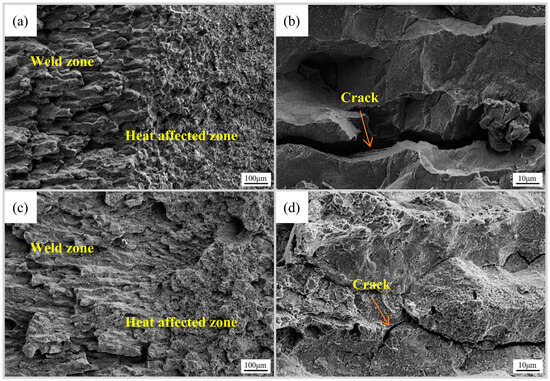
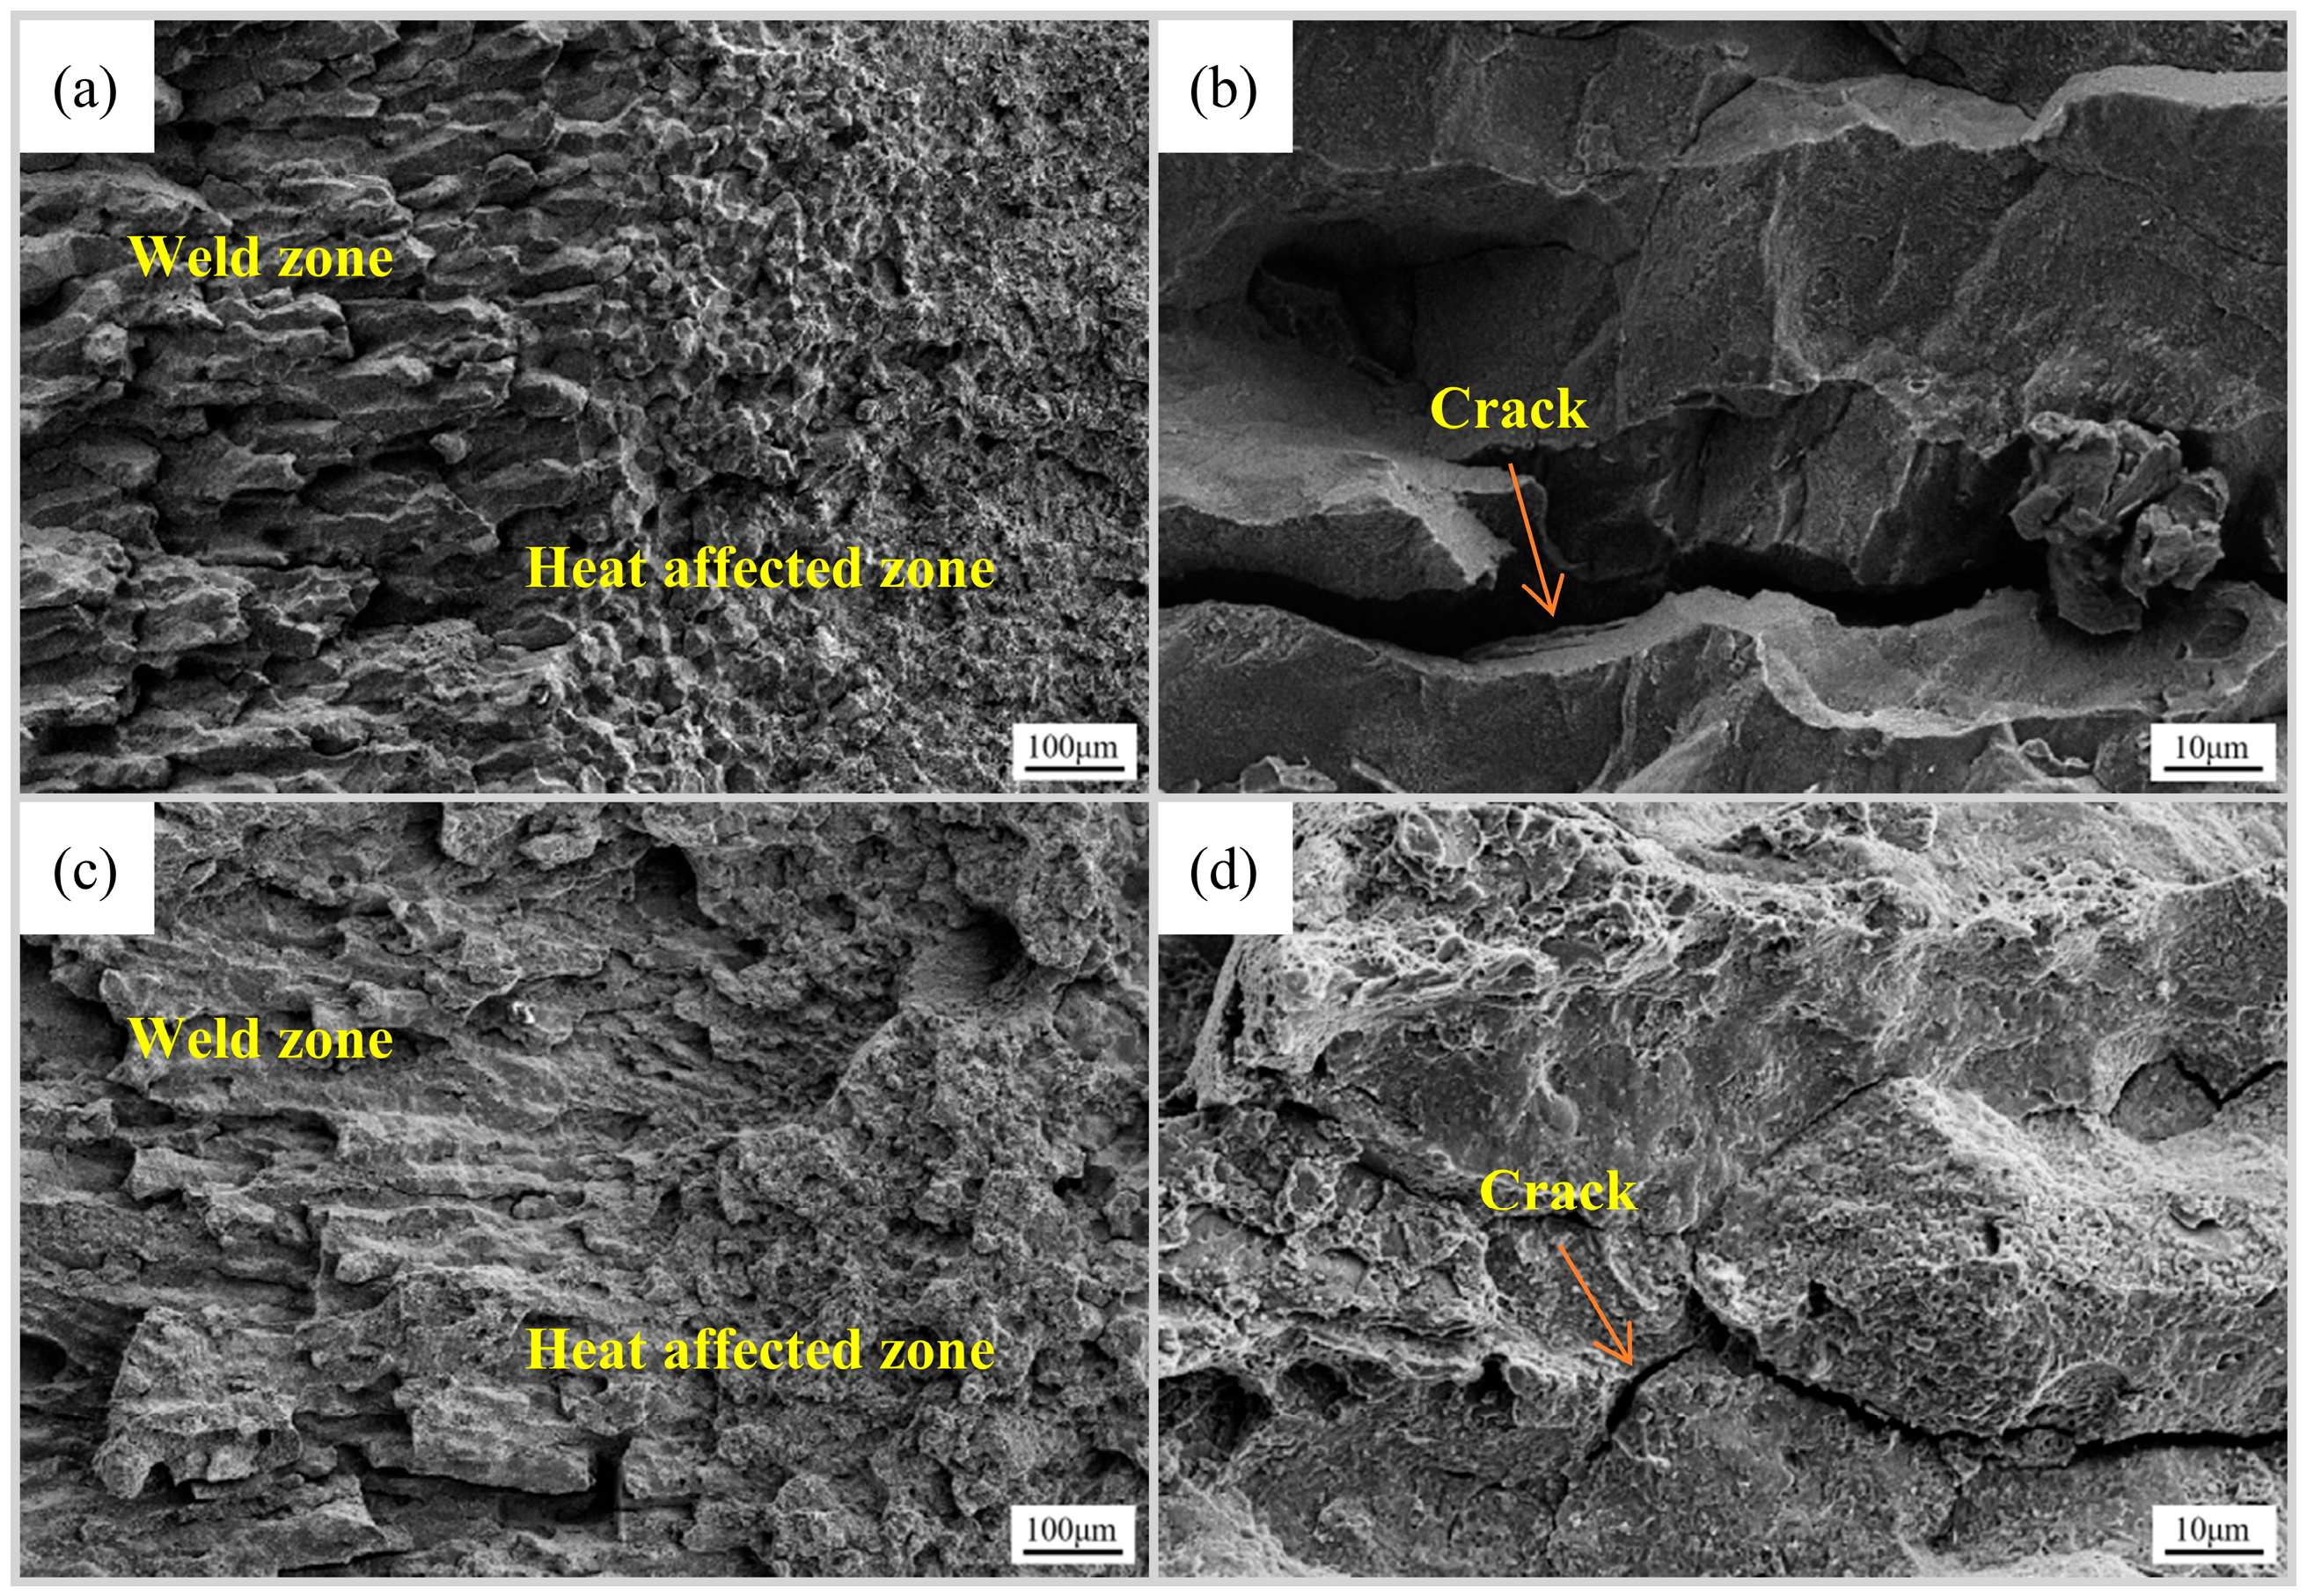
Because the same welding parameters were used, the HAZ of the welded joints produced using the three types of welding wire were essentially the same. Figure 17 shows the SEM morphology of the impact fracture surface of a welded joint produced using LC welding wire. As can be seen from Figure 17a,b, there is a marked difference in the microstructure of the weld and the HAZ in the post-weld tempered impact fracture of the LC welding wire; the weld zone exhibits coarse columnar grains, while the fracture surface shows intergranular cracks, indicating a typical brittle fracture. Figure 17c,d shows the impact fracture surfaces of the LC welding wire after quenching and tempering. It can be seen that the columnar grain morphology in the weld zone has disappeared, and there are distinct laminar tear ridges on the fracture surface. The local fracture facets exhibit numerous fine ductile dimples, indicating good toughness. Due to the low carbon content of the LC welding wire, the microstructure of the weld metal becomes non-uniform after post-weld quenching and tempering, and the hardness of the weld metal is lower than that of the base material. However, the low-carbon lamellar martensite in the weld metal exhibits good toughness; consequently, the welded joint as a whole demonstrates relatively good impact toughness.
Figure 17.
SEM morphology of impact fracture of LC welding wire welded joint: (a,b) LC-TT weld area; (c,d) LC-AQT weld area.
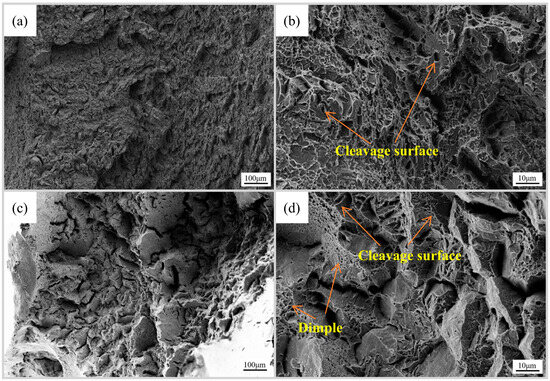
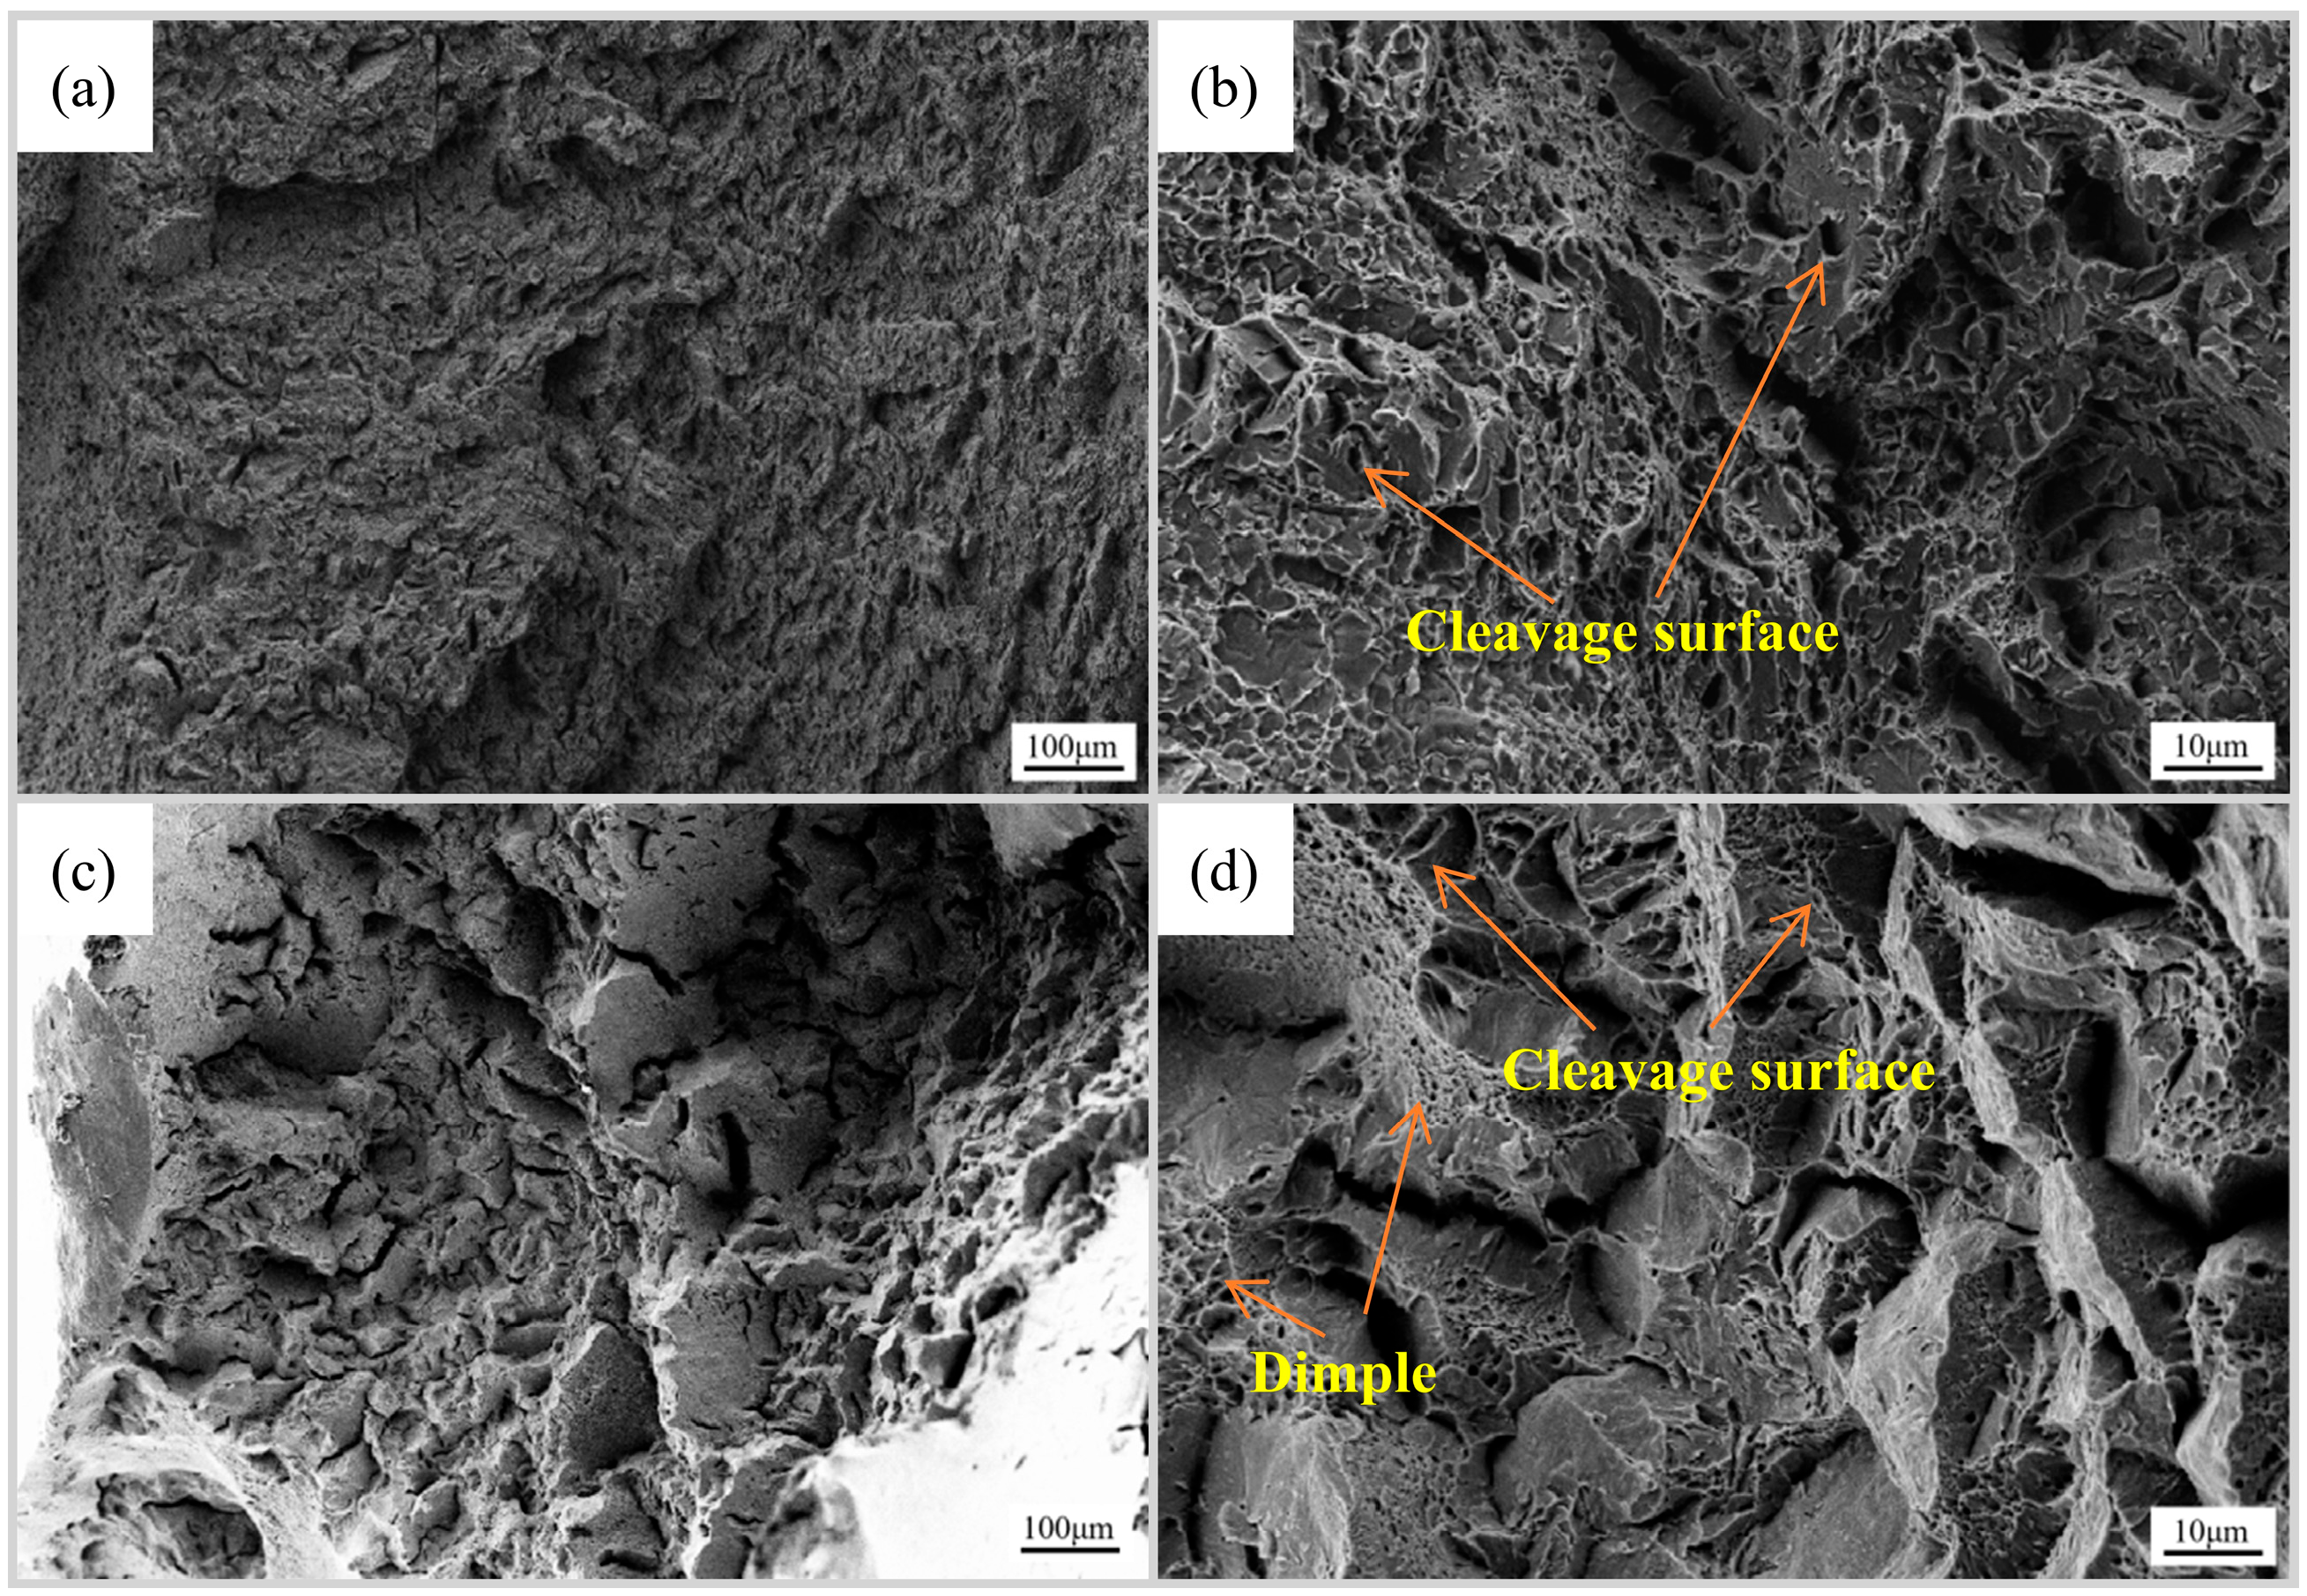
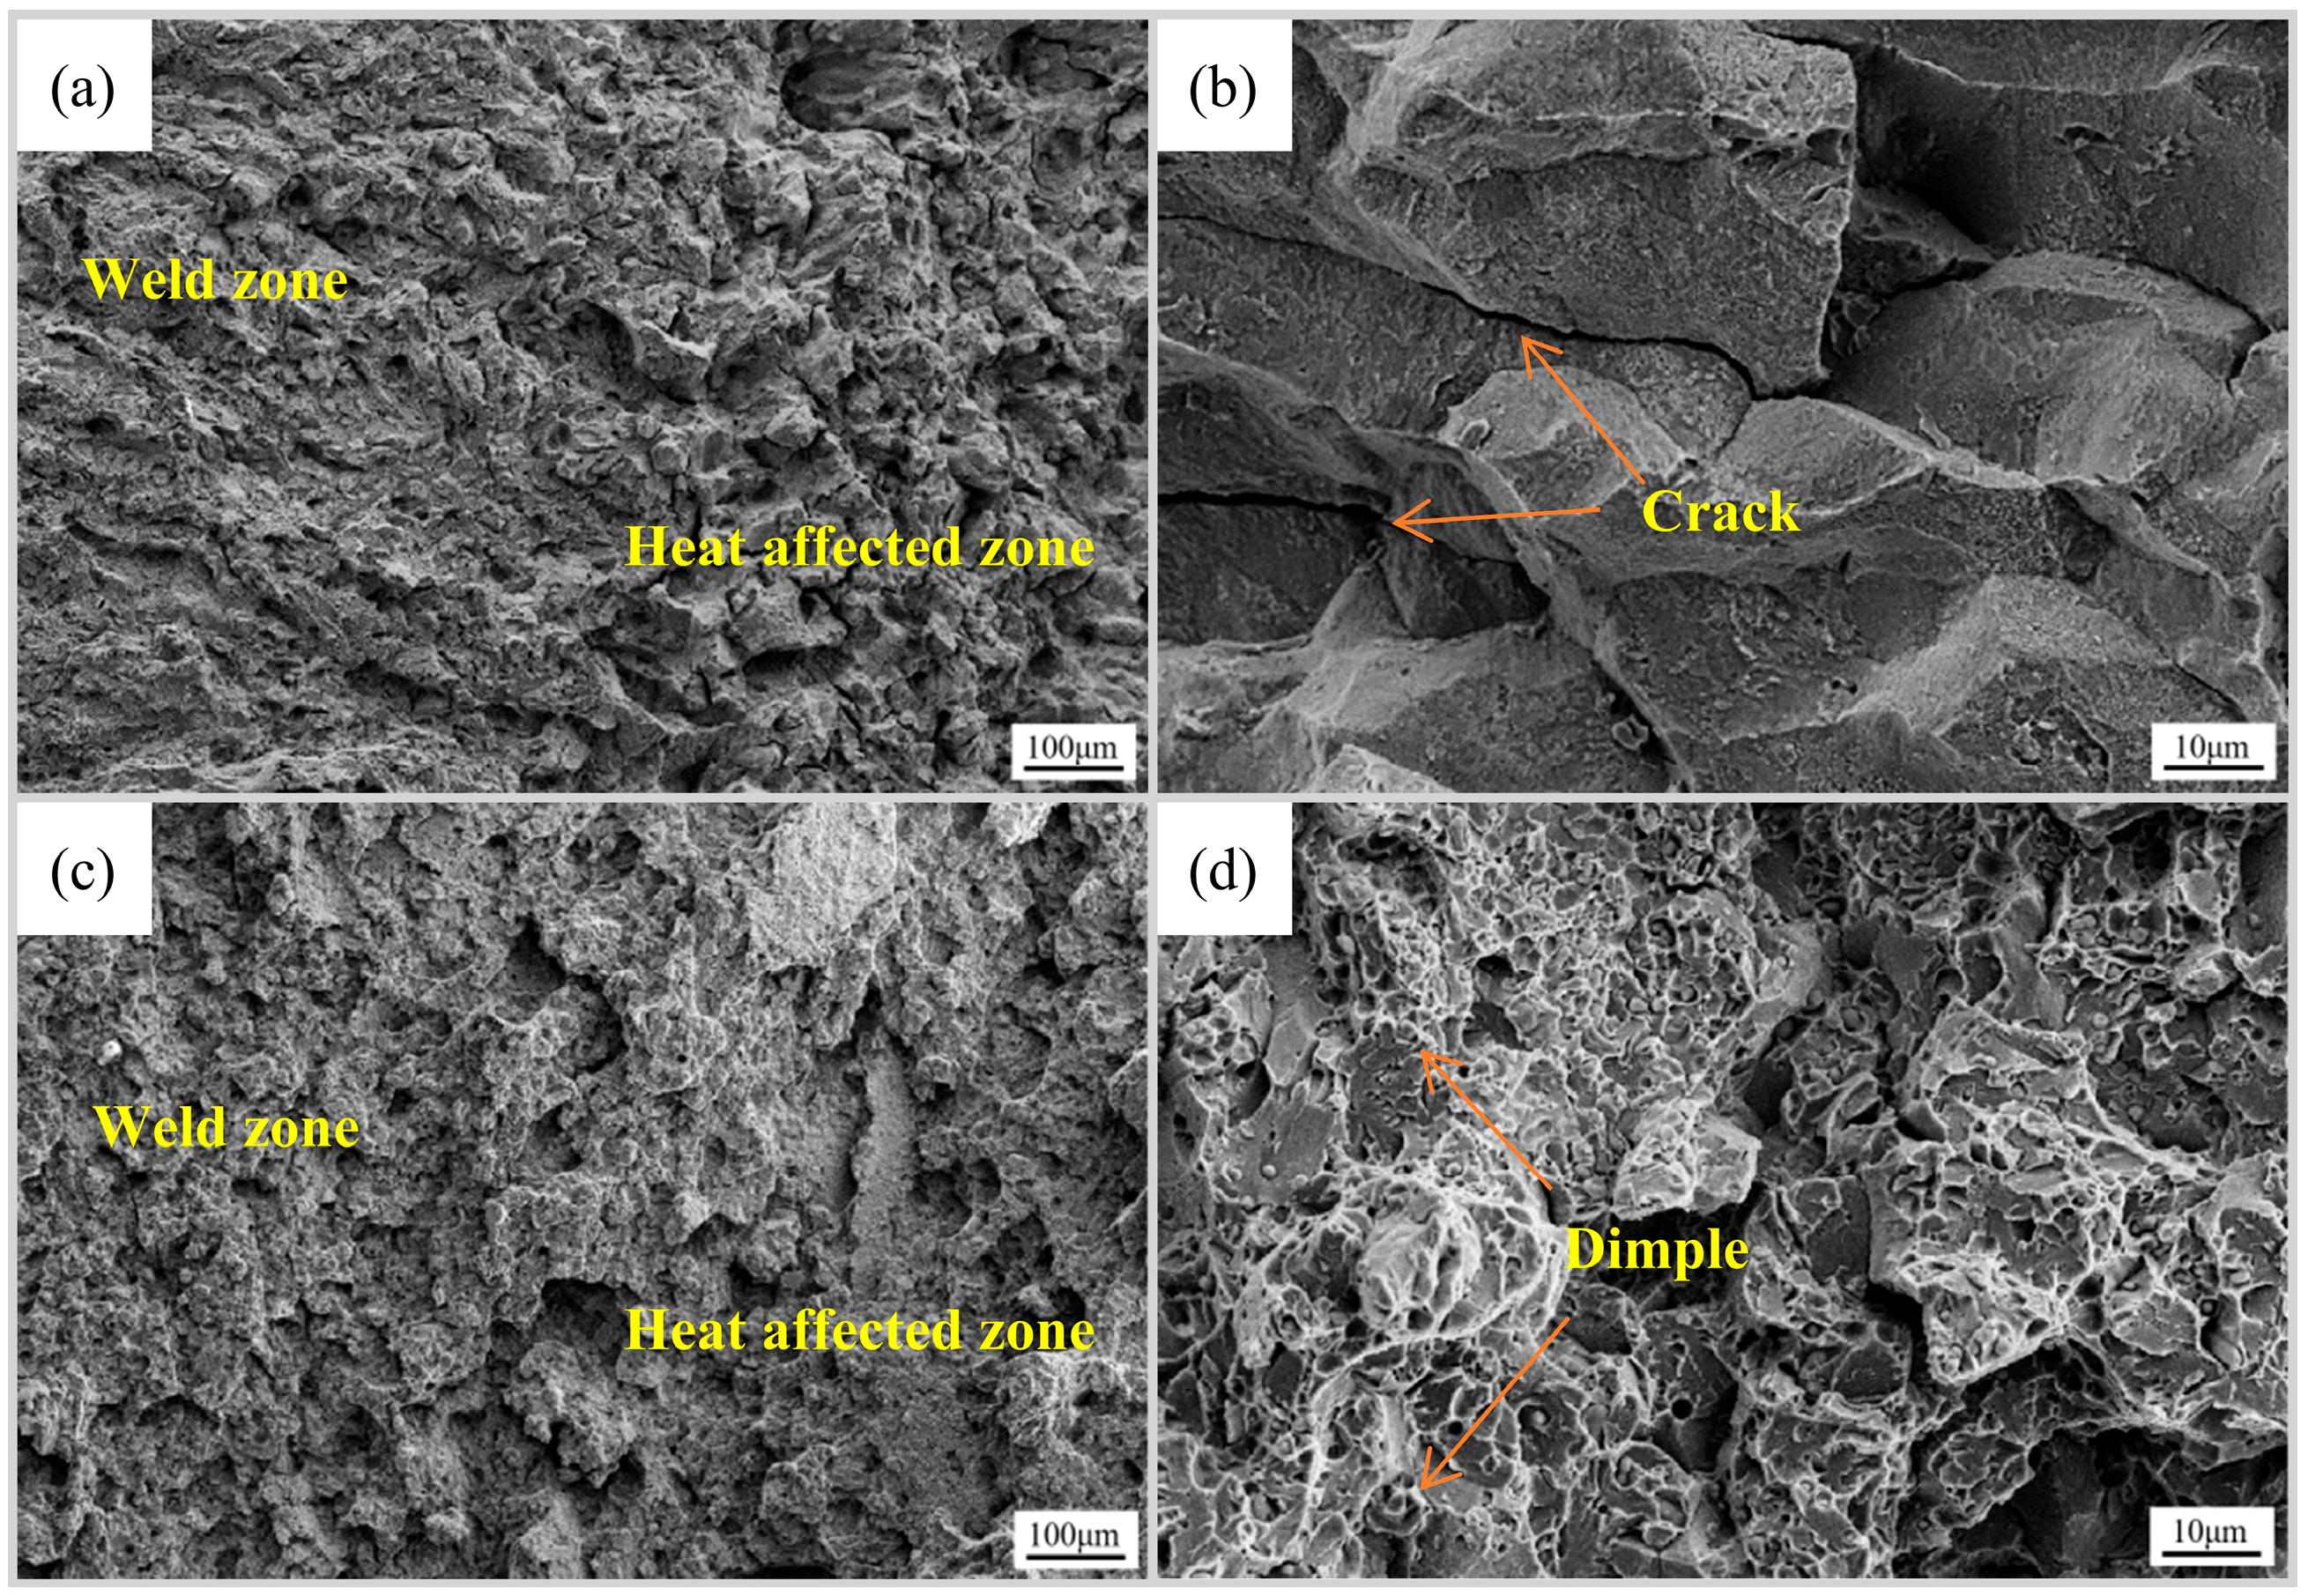
Figure 18 shows the SEM morphology of the impact fracture surface of a welded joint produced using BM welding wire. As can be seen from Figure 18a,b, there is a marked difference between the weld metal and the adjacent HAZ in the fracture surfaces of the impact test specimens from the BM welded joint after post-weld tempering; the weld metal exhibits typical intergranular brittle fracture characteristics, with distinct grain boundary fracture surfaces and locally flat, smooth fracture surfaces. The impact fracture surface of BM welding wire following quenching and tempering still retains the differences in morphology between the original weld and the HAZ, as shown in Figure 18c,d. The fracture surface in the weld zone exhibits small cleavage steps in places, with no smooth fracture facets, indicating a brittle fracture. The BM-TT joint exhibited the lowest impact energy (10.3 J). This low toughness is consistent with the fracture morphology observed in the BM-TT specimen. The weld metal retained a pronounced columnar morphology, and the impact fracture exhibited locally flat regions and intergranular brittle-fracture characteristics. Such a fracture path provides limited resistance to crack propagation and is therefore consistent with the low absorbed impact energy. Although the BM wire has a nominal composition matching the base metal, composition matching alone does not eliminate the heterogeneous weld-metal morphology generated during fusion welding. The post-weld tempering treatment in the TT route also differs from the quenching-and-tempering route in its ability to re-establish a more uniform transformed microstructure. Accordingly, the low BM-TT impact energy is attributed to the observed brittle weld-metal fracture behavior and microstructural heterogeneity rather than to a single independently verified mechanism.
Figure 18.
SEM morphology of impact fracture of BM welding wire welded joint: (a,b) BM-TT weld area; (c,d) BM-AQT weld area.
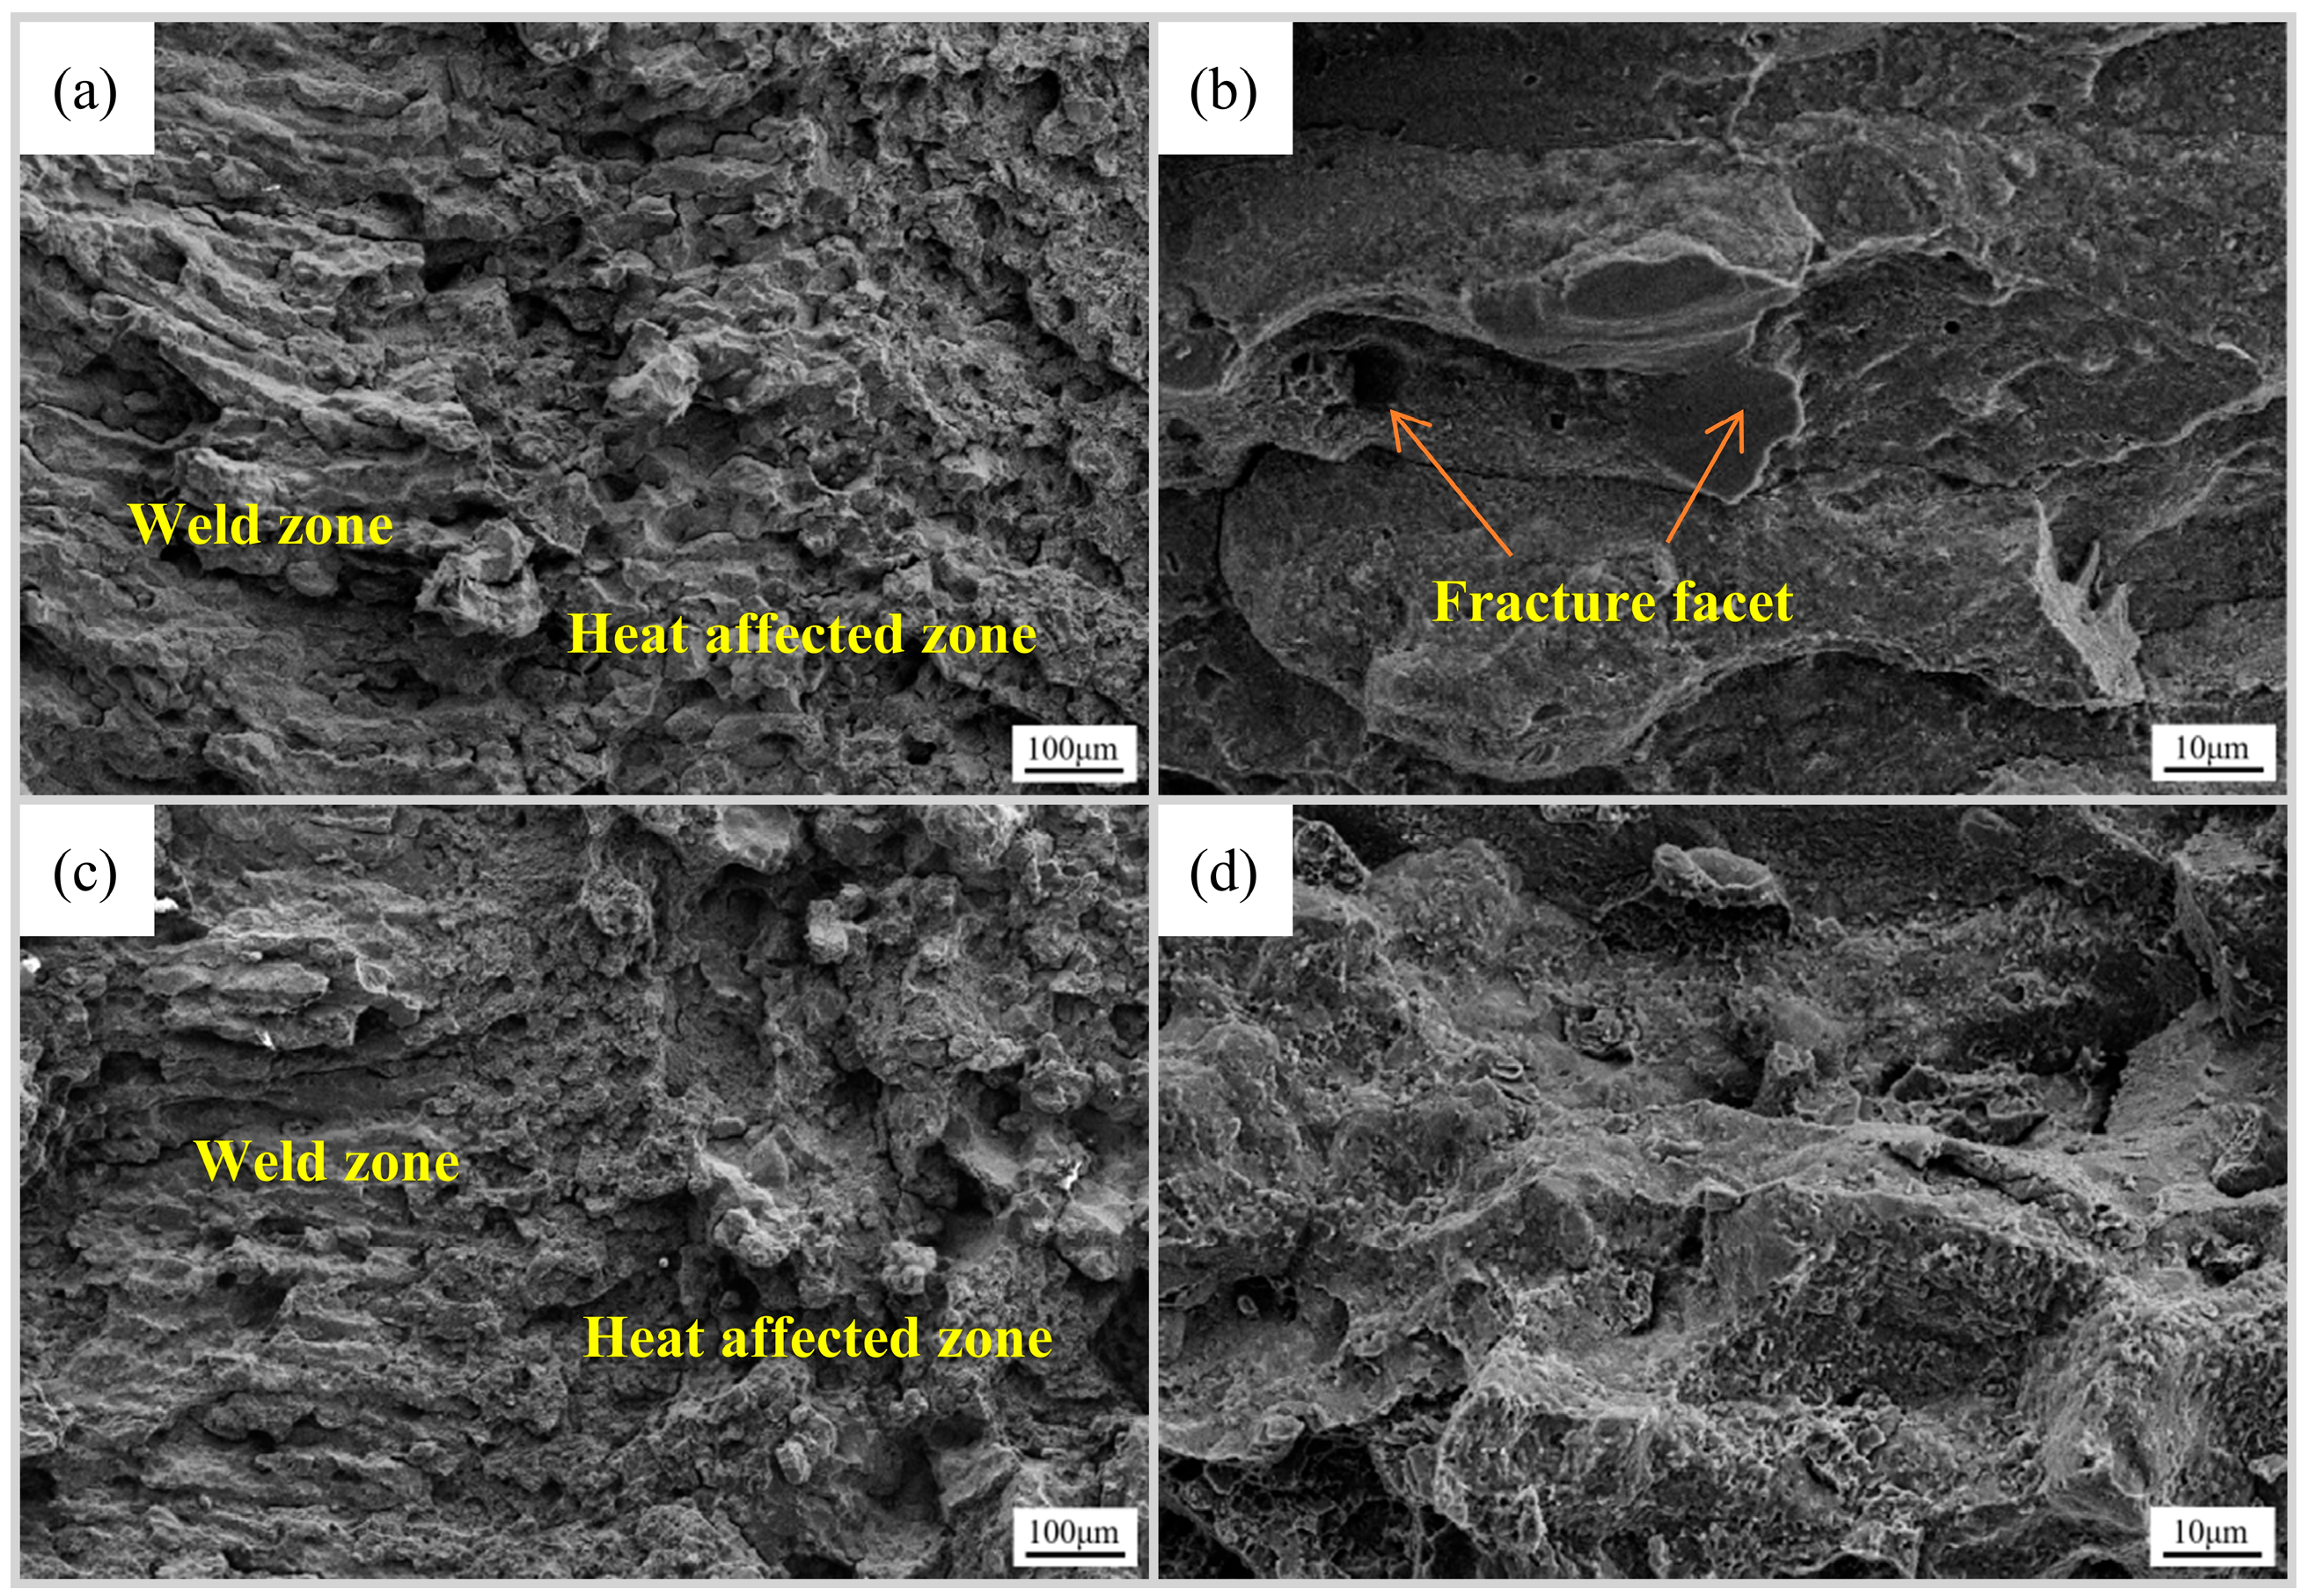
Figure 19 shows the SEM morphology of the impact fracture surface of a welded joint produced using HM welding wire. Figure 19a shows the low-magnification morphology of the weld region. It can be seen that there is a marked difference in the fracture morphology between the weld metal and the base material; the weld metal exhibits a distinct columnar grain structure, with coarse grains aligned in a specific direction. Figure 19b shows a close-up view of the weld metal. It can be seen that the weld metal exhibits coarse columnar grains, with cracks propagating along grain boundaries, indicating clear intergranular brittle fracture characteristics. As can be seen from Figure 19c,d, the grain size in the weld metal is coarse, and the crack propagation direction is consistent with the orientation of the columnar grains. Furthermore, the fracture surface is uneven, with some small tear ridges visible on the fracture surface. Compared with the post-weld tempered specimen (Figure 19b), the quenched and tempered specimen exhibits better toughness; however, the fracture mode remains predominantly intergranular brittle fracture.
Figure 19.
SEM morphology of impact fracture of HM welding wire welded joint: (a,b) HM-TT weld area; (c,d) HM-AQT weld area.
4. Conclusions
- (1)
- Post-weld quenching and tempering markedly improved hardness uniformity by reducing the hardness gradient. The weld metal hardness followed HM > BM > LC, while BM showed the closest hardness match to the base metal and the lowest hardness variation.
- (2)
- Compared with post-weld tempering, quenching and tempering significantly improved the overall mechanical properties. The tensile strengths of HM, LC, and BM joints reached 1299.5, 1315.6, and 1300.0 MPa, respectively, comparable to the base metal (1290.8 MPa). Impact toughness followed LC > HM > BM, with LC-AQT achieving the highest impact energy of 116.3 J.
- (3)
- Fracture morphology was consistent with the impact results. BM joints exhibited predominantly intergranular brittle fracture, while HM joints retained mainly brittle fracture characteristics. In contrast, LC-AQT exhibited numerous fine ductile dimples, indicating improved fracture toughness.
- (4)
- This study provides a comparative basis for selecting filler wires and post-weld heat-treatment routes for 4Cr13 steel repair welding. BM-AQT provides the best hardness matching and uniformity, whereas LC-AQT offers the highest elongation and impact toughness, indicating that filler-wire selection should be tailored to the targeted combination of mechanical properties.
Author Contributions
Conceptualization, Z.D.; methodology, Z.D. and C.Y.; investigation, Y.L., H.L. and Z.W.; formal analysis, Y.L. and L.P.; data curation, Y.L. and L.P.; validation, H.L.; visualization, Z.W.; writing—original draft, Z.D.; writing—review and editing, J.L., P.Z. and S.J.; software, C.Y. and J.L.; resources, S.J.; supervision, J.L., P.Z. and S.J.; project administration, P.Z.; funding acquisition, P.Z. and S.J. All authors have read and agreed to the published version of the manuscript.
Funding
This work is supported by the Basic Scientific Research Program of NIM (AKYZZ2540, AKYKF2626) and the Innovation and Entrepreneurship Training Program for Undergraduates at Jiangsu University of Science and Technology (X2026102890596).
Data Availability Statement
The original contributions presented in this study are included in the article; further inquiries can be directed to the corresponding authors.
Conflicts of Interest
The authors declare no conflicts of interest.
Abbreviations
The following abbreviations are used in this manuscript:
| TIG | Tungsten inert gas |
| HM | High-molybdenum welding wire |
| LC | Low-carbon welding wire |
| BM | Base-metal welding wire |
| DCEN | Direct current electrode negative |
| A | Annealed base material, as-welded |
| AQT | Annealed base material, quenched and tempered after welding |
| T | Tempered base material, as-welded |
| TT | Tempered base material, tempered after welding |
| OM | Axio Lab. A1 metallurgical microscope |
| SEM | Zeiss Supra 40 scanning electron microscope |
| HAZ | Heat-affected zone |
References
- Liu, J.Z.; Jia, Z.; Zhang, C.; Ren, B.; Wang, Y.J.; Zhao, Z.X.; Yang, L.K.; Mu, D.K. Microstructure Evolution Mechanism of 4Cr13 Steel During Thermal Deformation. Coatings 2026, 16, 383. [Google Scholar] [CrossRef] [Scilit]
- Salahi, S.; Kazemipour, M.; Nasiri, A. Effects of Microstructural Evolution on the Corrosion Properties of AISI 420 Martensitic Stainless Steel During Cold Rolling Process. Mater. Chem. Phys. 2020, 258, 123916. [Google Scholar] [CrossRef] [Scilit]
- Fan, Y.; Zhou, J.; Gu, J.B.; Chi, H.X.; Ma, D.S.; Xie, G.L.; Di Schino, A. Effect of N on the Microstructure and Wear Resistance of 4Cr13 Corrosion-Resistant Plastic Mold Steel. Materials 2024, 18, 308. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Gao, J.S.; Lan, H.X.; Jiang, Q.S.; Chen, S.Q.; Xu, Z.L.; Yu, Y.C.; Du, X.L.; Cai, L.Z. Mechanisms of Hardness Variation in 14Cr12Ni3Mo2VN Martensitic Stainless Steel Under Different Tempering Temperatures Following High-Frequency Induction Quenching. Coatings 2025, 15, 306. [Google Scholar] [CrossRef] [Scilit]
- Lyu, Z.; Long, B.E.; Lienert, T.J.; Li, L. Effects of Preheating on the Microstructure of Laser-DED AISI 420. Weld. J. 2024, 103, 372–377. [Google Scholar] [CrossRef] [Scilit]
- Dunne, D.; Li, H.J.; Pereloma, E. Effect of Inter-Pass Temperature and Time on Martensite Formation in the Heat-Affected Zone During Multi-Pass Welding of P91 Steel. Metals 2025, 15, 501. [Google Scholar] [CrossRef] [Scilit]
- Li, L.; Guo, S.D.; Guo, Y.H.; Ren, J.Z.; Hou, W.B.; Wang, X.G.; Jia, L.; Zhang, N.N.; Gan, H.Y. Effect of Laser Shock Processing on Residual Stress Evolution in Martensitic Stainless Steel Multi-Pass Butt-Welded Joints. Mater. Res. Express 2023, 10, 034003. [Google Scholar] [CrossRef] [Scilit]
- Yelbay, H.I.; Gür, C.H. Non-Destructive Determination of Surface Residual Stresses in Electron Beam Welded AISI 410 Martensitic Stainless Steel Using the Magnetic Barkhausen Noise Technique. Metals 2025, 15, 305. [Google Scholar] [CrossRef] [Scilit]
- Liu, P.; Ma, J.; Fang, Y.T.; Xu, B.W.; Qiu, L. Effect of Repeated Weld Repairs on Microstructure and Mechanical Properties of Heat-Affected Zone in CA6NM Stainless Steel. Adv. Mater. Sci. Eng. 2022, 2022, 4527917. [Google Scholar] [CrossRef] [Scilit]
- Yelamasetti, B.; Karuna, B.N.R.; Vardhan, T.V.; Dasore, A.; Saxena, K.K.; Faroque, F.A.; Revathi, V.; Abduvalieva, D. Mechanical and Micro-Structural Studies of Pulsed and Constant Current TIG Weldments of Super Duplex Stainless Steels and Austenitic Stainless Steels. High Temp. Mater. Process. 2024, 43, 20240003. [Google Scholar] [CrossRef] [Scilit]
- Gurav, V.; Shrivastava, D. Optimization of Mechanical Properties and Microstructure Characterization of Resistance Spot Welded Martensitic Stainless Steel: In-Situ Tempering and TLBO Approach. Sci. Rep. 2026, 16, 12989. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Sommer, N.; Stredak, F.; Wiegand, M.; Boehm, S. Grain Growth and Precipitation Behaviour of AISI 430 ferritic stainless steel Subjected to Pulsed Laser Beam Welding Using Free-Form Pulse Shaping. Weld. World 2022, 67, 51–62. [Google Scholar] [CrossRef] [Scilit]
- Hosseini, M.M.; Lanteigne, J.; Baillargeon, C.; Jahazi, M.; Champliaud, H. Development of a Flow Rule Based on a Unified Plasticity Model for 13Cr-4Ni Low-Carbon Martensitic Stainless Steel Subject to Post-Weld Heat Treatment. Metals 2024, 14, 834. [Google Scholar] [CrossRef] [Scilit]
- Wan, Y.; Song, L.M.; Xie, X.F.; Shi, Y. Evolution of Residual Stress and Microstructure of 2205 Duplex Stainless Steel Welded Joints During Different Post-Weld Heat Treatment. High Temp. Mater. Process. 2024, 43, 20240027. [Google Scholar] [CrossRef] [Scilit]
- Sisodia, R.P.S.; Gaspar, M. Investigation of Metallurgical and Mechanical Properties of Laser Beam Welded and Post-weld Heat Treated DP1400 Steel. J. Mater. Eng. Perform. 2021, 30, 1703–1710. [Google Scholar] [CrossRef] [Scilit]
- Triani, R.M.; Neto, J.B.T.D.R.; De Oliveira, P.G.B.; Rego, G.C.; Neto, A.L.; Casteletti, L.C. In-Situ Production of Metal Matrix Composites Layers by TIG Surface Alloying to Improve Wear Resistance of Ductile Cast Iron Using a Buffer-Layer and Post Weld Heat Treatment. Coatings 2023, 13, 1137. [Google Scholar] [CrossRef] [Scilit]
- Yang, H.W.; Chen, J.M.; Zhao, X.Y.; Huda, N.; Gerlich, A.P. Effect of Filler Wire Composition on Weld Metal Microstructure and Mechanical Properties in X80 Steel Laser Welds. Materials 2024, 17, 5235. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Bansod, A.; Shukla, S.; Gahiga, G.; Verma, J. Influence of Filler Wire on Metallurgical, Mechanical, and Corrosion Behaviour of 430 Ferritic Stainless Steel Using a Fusion Welding Process. Mater. Res. Express 2023, 10, 036513. [Google Scholar] [CrossRef] [Scilit]
- Gupta, A.; Singh, J.; Chhibber, R. Dissimilar Welding of Austenitic and Ferritic Steels Using Nickel and Stainless-Steel Filler: Associated issues. Proc. Inst. Mech. Eng. E J. Process Mech. Eng. 2024, 238, 2524–2544. [Google Scholar] [CrossRef] [Scilit]
- Tembhurkar, C.; Ambade, S.; Kataria, R.; Verma, J.; Moon, A. Cold Metal Transfer Welding of 316L/430 Dissimilar Stainless-Steel Welds. Anti-Corros. Methods Mater. 2025, 72, 178–188. [Google Scholar] [CrossRef] [Scilit]
- Wang, K.; Gao, G.H.; Gui, X.L.; Bai, B.Z.; Feng, C. Comparison of Microstructure and Mechanical Properties of a High-Carbon Bainitic Steel Treated by Long-Time Bainitic Austempering and Short-Time Austempering Plus Tempering Processes. Steel Res. Int. 2024, 95, 2300501. [Google Scholar] [CrossRef] [Scilit]
- Karthick, K.; Malarvizhi, S.; Balasubramanian, V. Microstructural Characterization of Dissimilar Weld Joint Between Ferritic Steel and Stainless Steel. Mater. Sci. Technol. 2021, 37, 1257–1269. [Google Scholar] [CrossRef] [Scilit]
- Meng, X.L.; Fan, X.Y.; Guo, Y.H. Measurement of Ce/Ti Content in Austenitic Stainless Steel Welding Wire. Steel Res. Int. 2019, 90, 1800376. [Google Scholar] [CrossRef] [Scilit]
- Feng, F.; Fu, Y.Q.; Ju, J.S. Unveiling the Mechanism of Heat-Input Control and Low-Carbon Welding Consumables on Suppression of Transition Zone Hard/Brittle Layers in Stainless Steel Clad Joints. Buildings 2026, 16, 975. [Google Scholar] [CrossRef] [Scilit]
- Kang, J.; Zhao, L.L.; An, T.B.; Cao, Z.L.; Zuo, Y.; Ma, C.Y. Effect of Carbon Content on Strength and Toughness of Deposited Metal for 1000 MPa-Grade High-Strength Welding Wire. Mater. Today Commun. 2024, 39, 108930. [Google Scholar] [CrossRef] [Scilit]
- Wei, W.; Huang, Z.Q.; Zhang, H.Y.; Guan, S.K. The Effect of W, Cr, Mo Content on the Microstructure and Mechanical Properties of the Weld Interface of TiC Cermet and Low-Carbon Steel. Coatings 2024, 14, 558. [Google Scholar] [CrossRef] [Scilit]
- GB/T 4340.1-2024; Metallic Materials—Vickers Hardness Test—Part 1: Test Method. The State Bureau of Quality and Technical Supervision: Beijing, China, 2024.
- GB/T 228.1-2021; Metallic Materials—Tensile Testing—Part 1: Method of Test at Room Temperature. The State Bureau of Quality and Technical Supervision: Beijing, China, 2021.
- GB/T 229-2020; Metallic Materials—Charpy Pendulum Impact Test Method. The State Bureau of Quality and Technical Supervision: Beijing, China, 2020.
- Duran, M.A.; Peitsch, P.; Svoboda, H.G. Phase Transformation Kinetics During Post-Weld Heat Treatment in Weldments of C-250 Maraging Steel. Materials 2025, 18, 2820. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Li, Q.; Wang, Q.; Zhang, L.; Chen, D.X.; Jin, H.; Li, J.D.; Zhang, J.W. Microstructure, Wear and Electrochemical Behaviors of Laser Cladding Fe-Based Coatings with Various Molybdenum Contents. Mater. Res. Express 2022, 9, 026504. [Google Scholar] [CrossRef] [Scilit]
- Guo, X.; Xu, K.; Wei, C.; Jiang, Y.L.; Lv, X.C.; Xu, Y.J. Effect of Mo in Ni-30Cr Filler Metal on the Eutectic Phases of Weld Metal. Weld. World 2023, 67, 1145–1153. [Google Scholar] [CrossRef] [Scilit]
- Kumar, H.; Banerjee, K.; Aqeel, M.; Shariff, S.M. Comparative Study of Diode Laser Welding of Solid-Solution/Precipitation-Strengthened Fe-Ni-Cr-Based Superalloys. Mater. Manuf. Process. 2025, 40, 1577–1589. [Google Scholar] [CrossRef] [Scilit]
- Liang, Y.; Wang, Q.; Song, Y.L.; Liu, Y.H. A New Designed Method for Evaluating the Repairability of a Newly Developed 5Cr5MoV Cold Working Die Steel. AIP Adv. 2021, 11, 035038. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.