


Abstract
This study examined the effects of laser shock peening (LSP) and LSP without protective coating (LSPwC) on the microstructure and corrosion behavior of 304L stainless steel using cyclic polarization testing. LSP enhanced corrosion resistance under mild sensitization (650 °C; 5 h) by inducing compressive stress and increasing dislocation density, stabilizing the passive film. Limited improvement was observed under severe sensitization (650 °C; 24 h). Deformation-induced martensite detected by XRD was attributed to mechanical polishing, not LSP. In contrast, LSPwC reduced corrosion resistance across all conditions due to Fe-rich surface oxides that impaired passivation.
1. Introduction
Austenitic stainless steels (SS) are widely recognized as one of the most versatile classes of materials due to their excellent mechanical properties, good formability, and high corrosion resistance. They are extensively used across a range of industries, with particularly critical applications in the nuclear sector. In nuclear reactor systems, these steels are commonly employed in piping, cladding, and structural components such as reactor core supports. They also serve a vital role in nuclear waste management as the primary material for fabricating nuclear storage canisters. These canisters form the backbone of dry cask storage systems (DCSS), which are designed to safely contain spent nuclear fuel (SNF) assemblies during their radioactive decay [1]. Among the available alloys, 304 and 316 stainless steels, along with their variants, are the most commonly used in DCSS applications.
A growing concern, however, is the potential for structural failure in these canisters due to material degradation. Localized corrosion and chloride-induced stress corrosion cracking (Cl-SCC) are well-documented failure mechanisms that can occur at the weldments of austenitic stainless steel DCSS canisters when exposed to chloride-rich aqueous environments [2,3,4,5]. Field inspections have confirmed that salt-bearing deposits can form on the surfaces of heated canisters near coastal storage sites [6,7,8,9]. As SNF decays, the canister surface temperature may fall within the threshold for deliquescence, depending on salt composition and ambient relative humidity [3,9,10,11,12].
Under these conditions, the resulting corrosive brine promotes pitting corrosion in stainless steel by forming a localized electrolyte enriched with chloride ions, which destabilize the passive film [12,13,14]. This susceptibility is further exacerbated if the alloy undergoes sensitization during fusion welding, as chromium depletion at grain boundaries caused by the precipitation of Cr-rich M23C6 carbides weakens the passive film near the heat-affected zone (HAZ) [15,16]. In addition, welding performed during the fabrication and repair of these canisters induces tensile residual stresses, as reported by Enos et al., further increasing the material’s susceptibility to both pitting and Cl-SCC [17,18].
In short, in-service 304L stainless steel canisters satisfy all the critical conditions for Cl-SCC: an aggressive environment, a susceptible microstructure, and the presence of tensile stress. This has prompted increased interest in surface modification techniques aimed at improving corrosion resistance in austenitic stainless steels. One promising method is laser shock peening (LSP), a non-contact surface treatment technique that uses high-energy, short-duration laser pulses to generate plasma-induced shock waves at the material surface. A transparent overlay is typically applied to confine the plasma, amplifying the pressure of the resulting shock wave as it propagates into the substrate. When this pressure exceeds the material’s Hugoniot Elastic Limit (HEL), it induces severe plastic deformation and generates a high density of dislocations in the near-surface region. These microstructural changes, including the development of deep compressive residual stresses and potential grain refinement, have been shown to improve the mechanical properties of austenitic stainless steels and enhance their corrosion resistance by stabilizing the passive film and reducing susceptibility to pitting and SCC.
This relationship between LSP-induced microstructural changes and improved corrosion resistance has been widely investigated in previous studies on austenitic stainless steels. Peyre et al. reported that LSP enhanced the corrosion resistance of 316L stainless steel by introducing compressive residual stresses that modified the alloy-defect interface and reduced the number of active sites for corrosion, thereby promoting a more stable passive film and improving resistance to both pitting and SCC in chloride-rich environments [19,20]. Similar results were observed by Lu et al. in 304 stainless steel, where LSP extended crack initiation times, increased pitting potentials, and reduced passive current densities [21,22]. These improvements were attributed to the combined effects of compressive residual stress and grain refinement, the latter of which enhances passive film stability through accelerated chromium diffusion and increases SCC resistance by promoting crack deflection or arrest at grain boundaries [21,22,23,24]. The extent of these benefits has been shown to increase with higher laser pulse densities due to greater residual compression and finer grain structures [21,25,26]. However, several studies have noted that these outcomes are not always consistent, underscoring the importance of optimizing LSP parameters to account for competing effects such as dislocation density, grain boundary characteristics, and the potential formation of deformation-induced martensite [27,28,29].
Building on previous research, this study evaluates the effects of laser shock peening, with and without a protective coating, on the corrosion resistance of sensitized 304L stainless steel in an oxidizing environment. While some prior work has explored the application of LSP without coating (LSPwC) on 304L stainless steel in chloride-rich environments [25,30,31,32], fewer studies have evaluated its performance in more oxidizing media like sulfuric acid. These environments offer greater sensitivity to changes in passivity, enabling a clearer assessment of LSP’s influence on passive film stability. It is hypothesized that LSP will enhance the corrosion resistance of 304L stainless steel by improving passive film stability through the introduction of compressive residual stresses. However, these beneficial effects may not be sufficient to fully counteract the detrimental impact of sensitization. In the case of LSPwC, performance is expected to decline due to surface oxidation caused by plasma-induced heating, which may impair passivity. These adverse effects may be mitigated at lower pulse energies where thermal influence is reduced.
The novelty of this study lies in the systematic comparison of LSP performed with and without a sacrificial coating under sensitized conditions, with particular emphasis on the interplay between residual stress, surface oxidation, and electrochemical corrosion response. Rather than proposing a new corrosion mechanism, this work clarifies the conditions under which LSP-induced mechanical benefits may be offset by surface chemistry effects, thereby providing practical guidance for the application of LSP in corrosion-sensitive environments.
2. Materials and Methods
2.1. Materials
Type 304L austenitic stainless steel plates, with a nominal thickness of 3 mm, were supplied by Sandia National Laboratories (Albuquerque, NM, USA). To achieve chemical homogeneity and dissolve pre-existing carbide precipitates, the hot-rolled plates were solution annealed at 1080 °C for 2 h and subsequently water quenched by the manufacturer. The bulk chemical composition, as provided by the supplier, is listed in Table 1.
Table 1.
Weight percent composition of 304L stainless steel.
2.2. Specimen Preparation
The stainless steel plates were sectioned into 30 mm × 30 mm square coupons using electrical discharge machining (EDM) to minimize thermal distortion and residual stress. All specimens were mechanically polished with silicon carbide (SiC) abrasive papers in sequential grit sizes ranging from 180 to 600 grit, producing a uniform surface finish. These initial specimens are referred to as the as-polished baseline (BL). To evaluate the effect of sensitization on corrosion behavior, two thermal exposure regimes were applied to separate sets of specimens. Sensitization was induced through isothermal heat treatment at 650 °C in ambient atmosphere for either 5 h (designated SEN1) or 24 h (designated SEN2), followed by air cooling. Table 2 summarizes the specimen designations and corresponding processing parameters.
Table 2.
Designation of specimens with parameters.
2.3. Laser Shock Peening
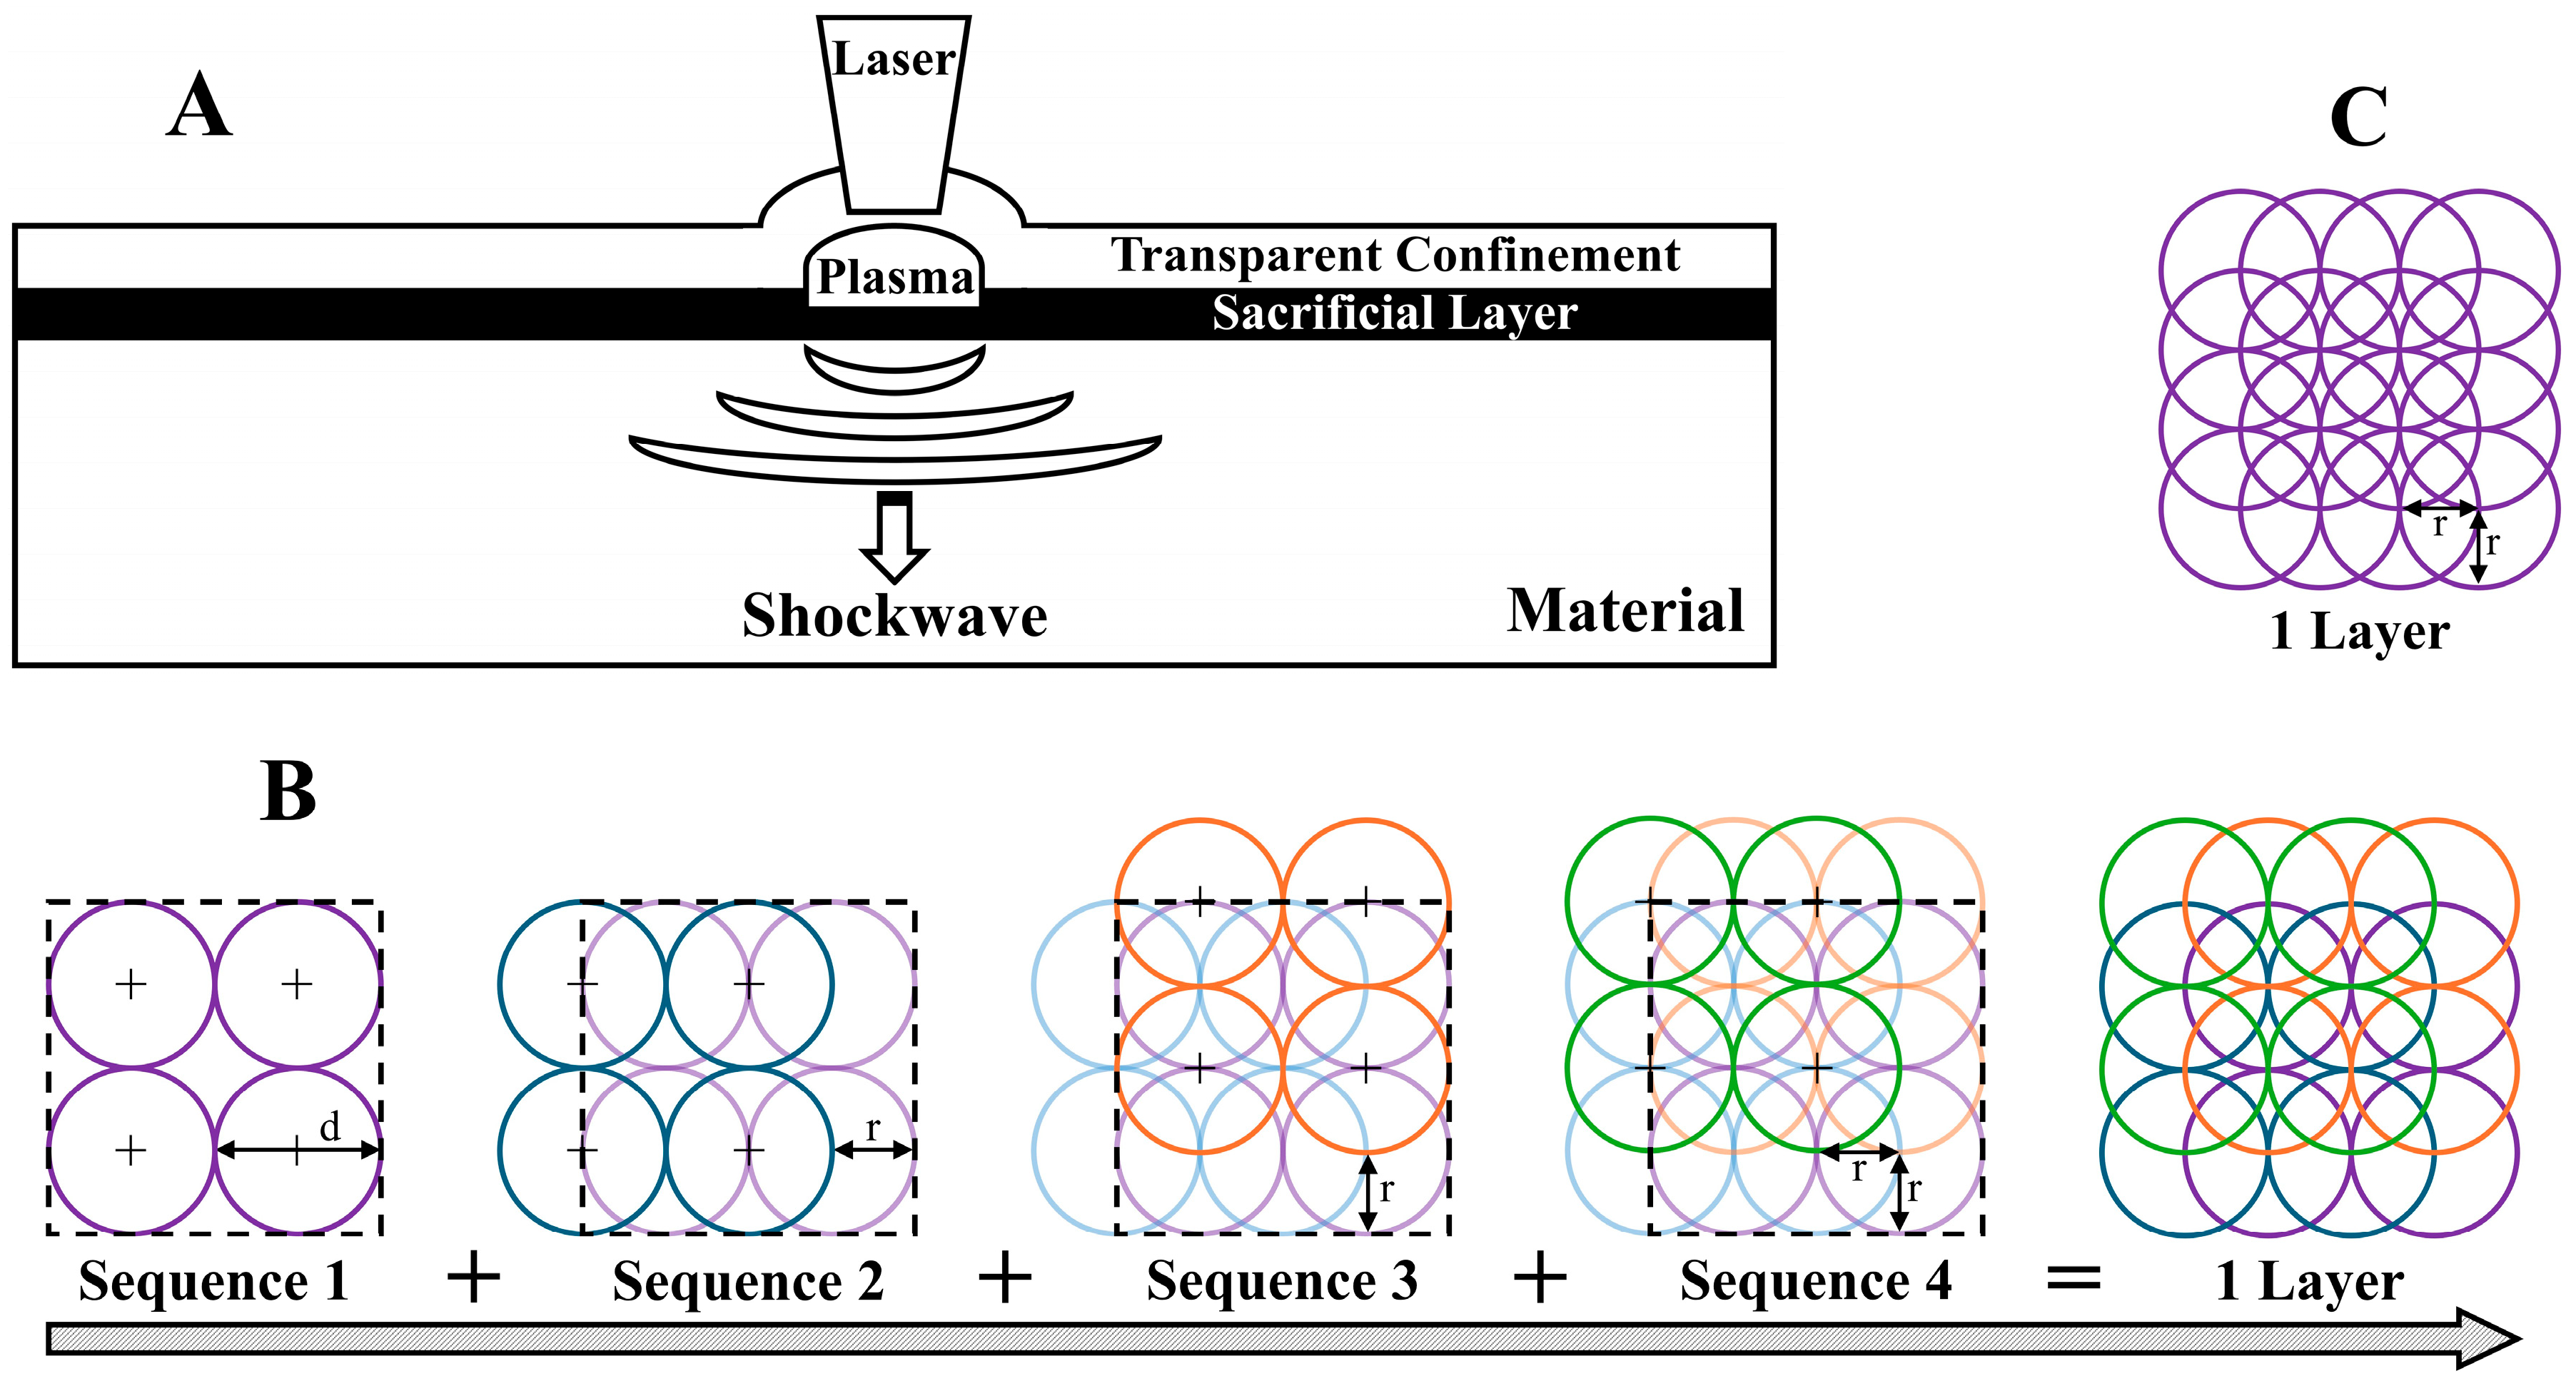
Laser shock peening (LSP) was performed at the University of Cincinnati using a Continuum Powerlite Plus system (Continuum, Santa Clara, CA, USA) equipped with a Q-switched Nd: YAG infrared laser (λ = 1064 nm), operating at 10 Hz with a maximum pulse energy of 3 J. The laser beam was focused to a 2 mm diameter spot size. Six LSP conditions were investigated to evaluate the effects of varying laser energy and the presence or absence of a sacrificial coating on corrosion behavior. These conditions consisted of three energy levels applied under two surface states: with (LSP) and without (LSPwC) a sacrificial coating. A summary of the key processing parameters is provided in Table 3, and the experimental setup and peening patterns are illustrated in Figure 1.
Table 3.
LSP Parameters.
Figure 1.
(A) Schematic of the LSP setup; (B) the four-pass sequence pattern used for LSP coated specimens; and (C) the single-pass sequence pattern used for uncoated LSPwC specimens.
Each LSP treatment targeted a 20 mm × 20 mm area and employed a 50% spot overlap strategy executed through four sequential passes to promote uniform coverage and a consistent residual stress distribution (Figure 1B). The laser path was precisely controlled by a Fanuc Robotics LR Mate 200iC system to maintain accurate spatial alignment between passes. A deviated spot pattern was used in each sequence to minimize tearing of the protective layer and to promote full-area coverage.
For the LSPwC conditions, a similar laser configuration was used; however, a direct 50% spot overlap was applied in a single pass (Figure 1C). This helps reduce cumulative energy input and excessive thermal accumulation at the surface, which may otherwise occur during direct laser–material interaction. In addition, this approach eliminates the need for multiple overlapping sequences and the additional step of applying a new sacrificial layer, providing potential advantages in process efficiency. The potential for simplified processing is a key motivation for investigating LSPwC.
Given these differences, variations in scanning strategy will likely result in different cumulative impact densities and energy inputs, while the presence or absence of a sacrificial layer further affects laser–surface interaction through energy attenuation. To maintain comparability between conditions, key laser parameters were held constant to reduce variability and achieve similar peak shock pressures. As such, differences between LSP and LSPwC reflect the combined effects of the sacrificial layer, scanning strategy, and laser–surface interaction.
For the LSP conditions, a 130 μm thick layer of 3M 471 black vinyl tape (3M, Maplewood, MN, USA) was applied to the specimen surface to reduce thermal effects and mitigate surface ablation. In contrast, LSPwC treatments were performed directly on the polished surface, allowing evaluation of laser-induced effects in the absence of a sacrificial layer. In both cases, a 1 mm thick water layer served as the transparent confining medium, amplifying the shock wave by constraining the plasma plume (Figure 1A) [33,34]. This process is known to induce severe plastic deformation (SPD) and deep compressive residual stresses near the surface.
2.4. Residual Stress Depth Profile
Residual stress (RS) and diffraction peak full width at half maximum (FWHM) were measured in two orthogonal directions (0° and 90°) using a Proto LXRD stress measurement system (Proto Manufacturing, Taylor, MI, USA) equipped with a single-axis goniometer operating in Ω geometry. Measurements were performed using the sin2ψ method with electrolytic layer removal. Prior to each run, the system was calibrated using certified 316L and carbon steel standards under Mn-Kα and Cr-Kα radiation, respectively, following ASTM E915-19 [35]. Depth profiling was conducted via sequential electropolishing using a solution of 87.5 vol% methanol and 12.5 vol% H2SO4. Material was removed in 30 μm increments up to 150 μm for high-resolution mapping near the surface, followed by 50 μm steps to 500 μm, 100 μm steps to 1100 μm, and 200 μm steps to a final depth of 1500 μm. Strain gradient and layer removal corrections were applied in accordance with SAE J784a [36]. LXRD measurement parameters are summarized in Table 4.
Table 4.
Proto LXRD residual stress measurement parameters for 304L stainless steel.
2.5. Cyclic Polarization Test
The degree of sensitization (DOS) and susceptibility to corrosion were determined by double-loop electrochemical potentiodynamic reactivation (DLEPR) using cyclic potentiodynamic polarization, in accordance with ASTM G108-94 [37]. Tests were conducted using a Gamry Reference 600 potentiostat (Gamry Instruments, Warminster, PA, USA) in a conventional three-electrode paracell configuration, with a graphite counter electrode, a reference saturated calomel electrode (SCE), and the target specimen as the working electrode. To minimize crevice corrosion along the O-ring, a Gamry electrolyte mask with a 1 cm2 porthole was applied to partially cover the specimen’s surface. The test solution consisted of 0.5 M H2SO4 + 0.05 M KSCN at 23 °C, prepared with deionized water and analytical-grade reagents. Potassium thiocyanate (KSCN) was added immediately before testing to minimize potential decomposition or contamination. Prior to each scan, the electrolyte was deaerated for 1 h using high-purity argon gas, followed by a 1 h stabilization period to reach a near steady-state open circuit potential (OCP). Cyclic polarization scans were carried out at a rate of 0.56 mV/s, sweeping the potential from −500 mV to +1000 mV (SCE) and then back to −500 mV.
It should be noted that the electrochemical tests were conducted as single measurements for several processing conditions. As a result, the reported electrochemical parameters are presented for comparative trend analysis rather than statistical evaluation. Future studies will incorporate replicate testing to enable quantitative assessment of variability.
2.6. Surface Optical Profile
Surface roughness was measured via white light vertical scanning interferometry using a Veeco Wyko NT1100 system (Veeco Metrology Group, Tucson, AZ, USA). A minimum of three scans were taken at randomly distributed locations across each specimen to ensure statistical consistency. Roughness parameters were extracted from the 3D profiles to assess surface modifications resulting from the LSP treatment.
2.7. Scanning Electron Microscopy
Microstructural analysis was conducted using an ThermoFisher Apreo field emission scanning electron microscope (SEM; ThermoFisher Scientific, Waltham, MA, USA) equipped with a solid-state detector for energy dispersive X-ray spectroscopy (EDS). Imaging was carried out in both secondary electron (SE) and backscattered electron (BSE) modes under an accelerating voltage of 20 kV, a beam current of 3.2 nA, and a working distance of 10 mm. In BSE imaging, channeling contrast predominated due to the similar atomic numbers of the alloying elements in 304L stainless steel, which limited compositional differentiation.
2.8. X-Ray Diffraction (XRD)
Phase analysis of the 304L stainless steel specimens was conducted using a PANalytical X’Pert Modular Powder Diffractometer (Malvern PANalytical, Almelo, The Netherland) with Cu-Kα radiation (λ = 1.5406 Å) operated in θ–2θ geometry. Diffraction patterns were collected over a 2θ range of 30–110° with a step size of 0.02° and a dwell time of 0.5 s per step. The resulting data were used to identify phase constituents and detect possible deformation-induced transformations.
3. Results
3.1. Microstructure Analysis and Surface Profile
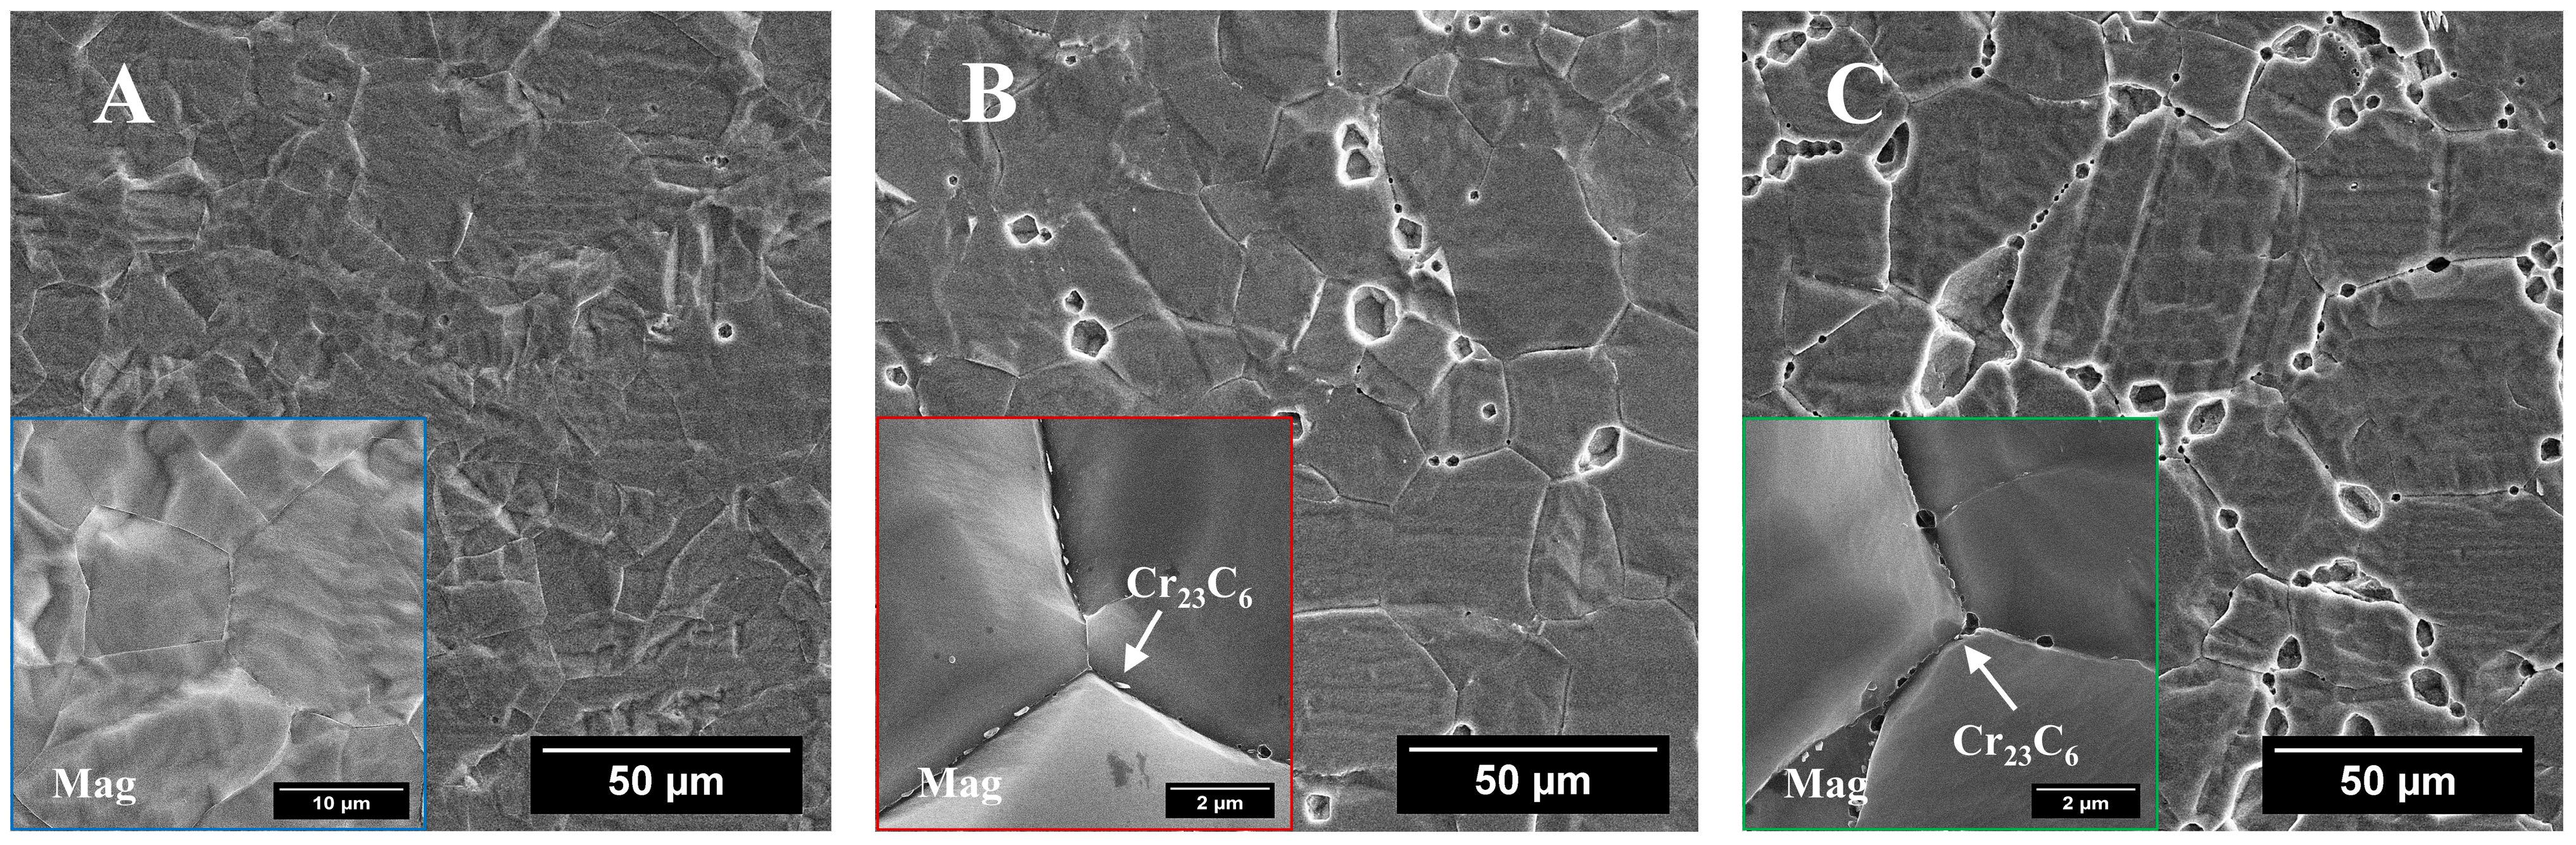
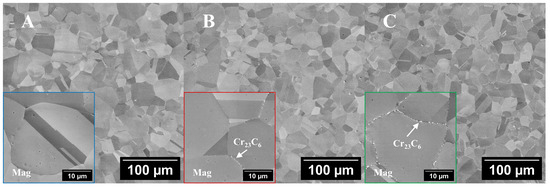
Figure 2 presents SEM secondary electron (SE) micrographs of as-polished 304L stainless steel in three conditions: the baseline (BL), and specimens sensitized at 650 °C for 5 h (SEN1) and 24 h (SEN2). Compared to BL, both SEN1 and SEN2 exhibit chromium-rich carbide precipitation along the grain boundaries, as confirmed by EDS analysis, with the extent of precipitation more pronounced in SEN2 due to prolonged exposure. This carbide formation is consistent with established literature and is linked to localized chromium depletion that weakens the passive film and increases susceptibility to intergranular corrosion (IGC) [16,38]. As a result, sensitized specimens are expected to exhibit higher degrees of susceptibility (DOS), especially in SEN2.
Figure 2.
SEM SE micrographs with magnification (Mag) of as-polished 304L stainless steel in three conditions: (A) BL; baseline, (B) SEN1; sensitized for 5 h, and (C) SEN2; sensitized for 24 h. Precipitation of chromium-rich carbides is observed along grain boundaries in SEN1 and SEN2.
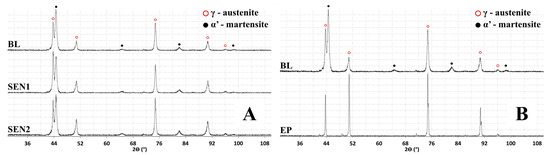
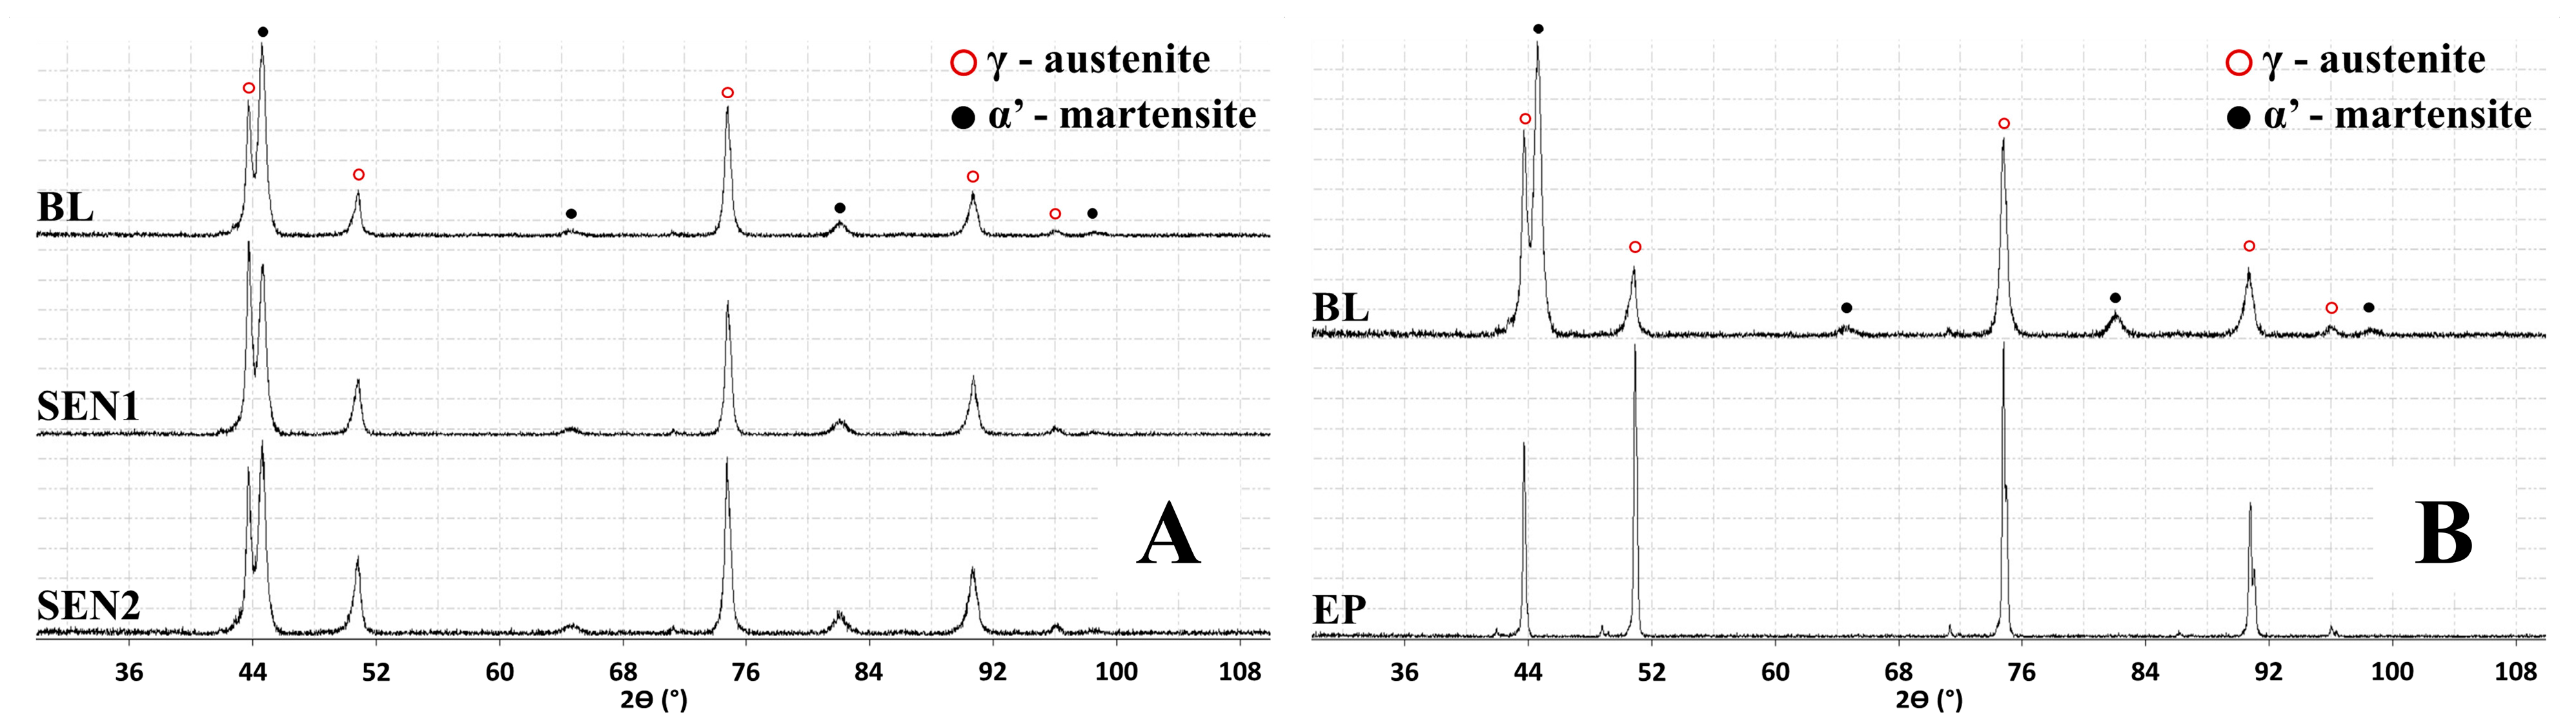
SEM imaging of the 304L stainless steel specimens revealed a predominantly equiaxed austenitic microstructure, with an average grain size of 16.25 μm ± 1.33 μm (ASTM grain size No. 9) [39], measured using the line intercept method in ImageJ (Version 1.54m). No evidence of grain coarsening was observed across the sensitization conditions, indicating that the applied thermal exposures had minimal effect on the bulk grain morphology. The microstructure showed no visible presence of secondary phases such as martensite or delta ferrite. However, XRD analysis of the as-polished surface (Figure 3A) revealed additional peaks corresponding to a body-centered cubic (BCC) phase, likely deformation-induced martensite. After electropolishing, these peaks disappeared (Figure 3B), confirming that the martensitic phase was confined to the mechanically worked surface layer generated during specimen preparation.
Figure 3.
(A) XRD patterns of as-polished BL, SEN1, and SEN2 specimens showing the presence of austenitic and martensitic phases. (B) XRD comparison of the BL specimen before and after electropolishing (EP), confirming that the martensitic phase was introduced during surface polishing.
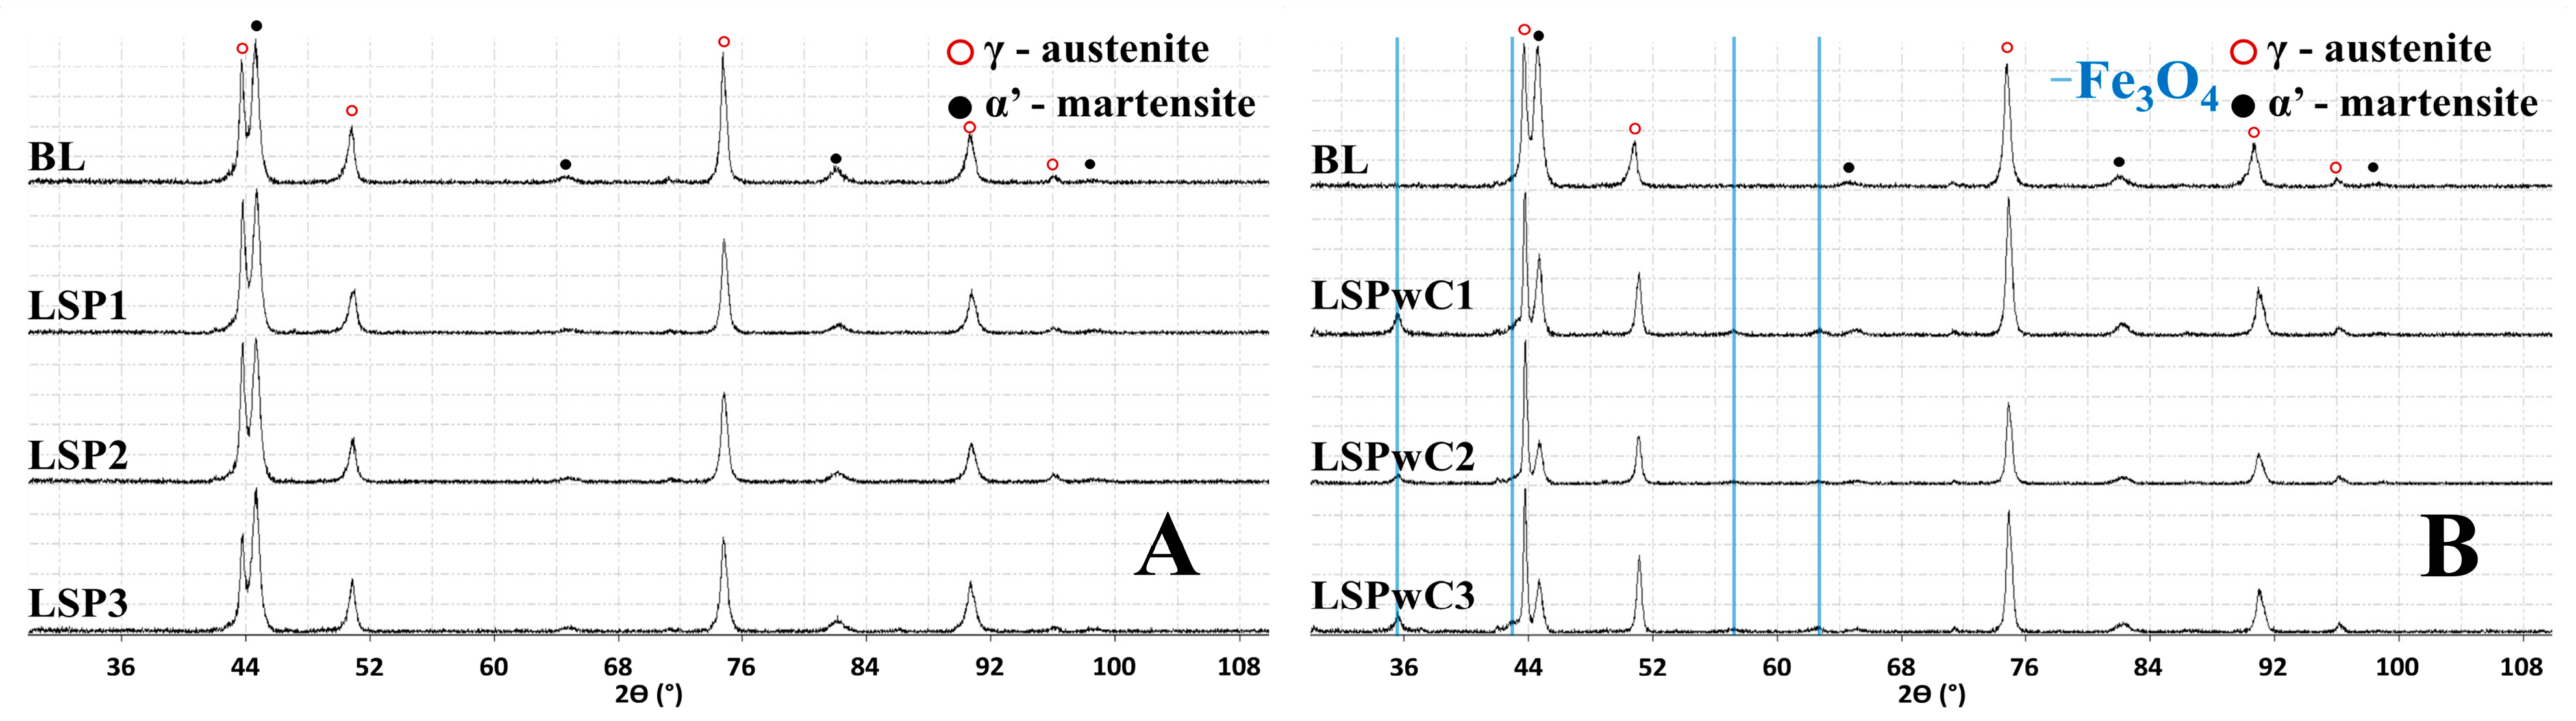
Following these results, XRD analysis of the laser-treated specimens revealed only minor phase changes related to surface modification. The LSP-treated samples remained predominantly austenitic, with a slight increase in deformation-induced martensite (Figure 4A). However, the martensitic phase was also detected in the BL specimen, suggesting that most of its formation likely resulted from mechanical polishing rather than laser processing. Table 5 summarizes the estimated martensite content after each treatment, calculated in accordance with ASTM E975-13 [40] using the (200)α’ and (220)γ peaks for comparison. In the LSPwC specimens, additional peaks corresponding to iron oxide phases, specifically Fe3O4, were observed in the XRD patterns (Figure 4B).
Figure 4.
XRD patterns of as-polished BL following (A) LSP; laser shock peening and (B) LSPwC; laser shock peening without coating. Iron oxide peaks were observed in the LSPwC-treated specimen.
Table 5.
Percentage of deformation-induced martensite following LSP surface treatment.
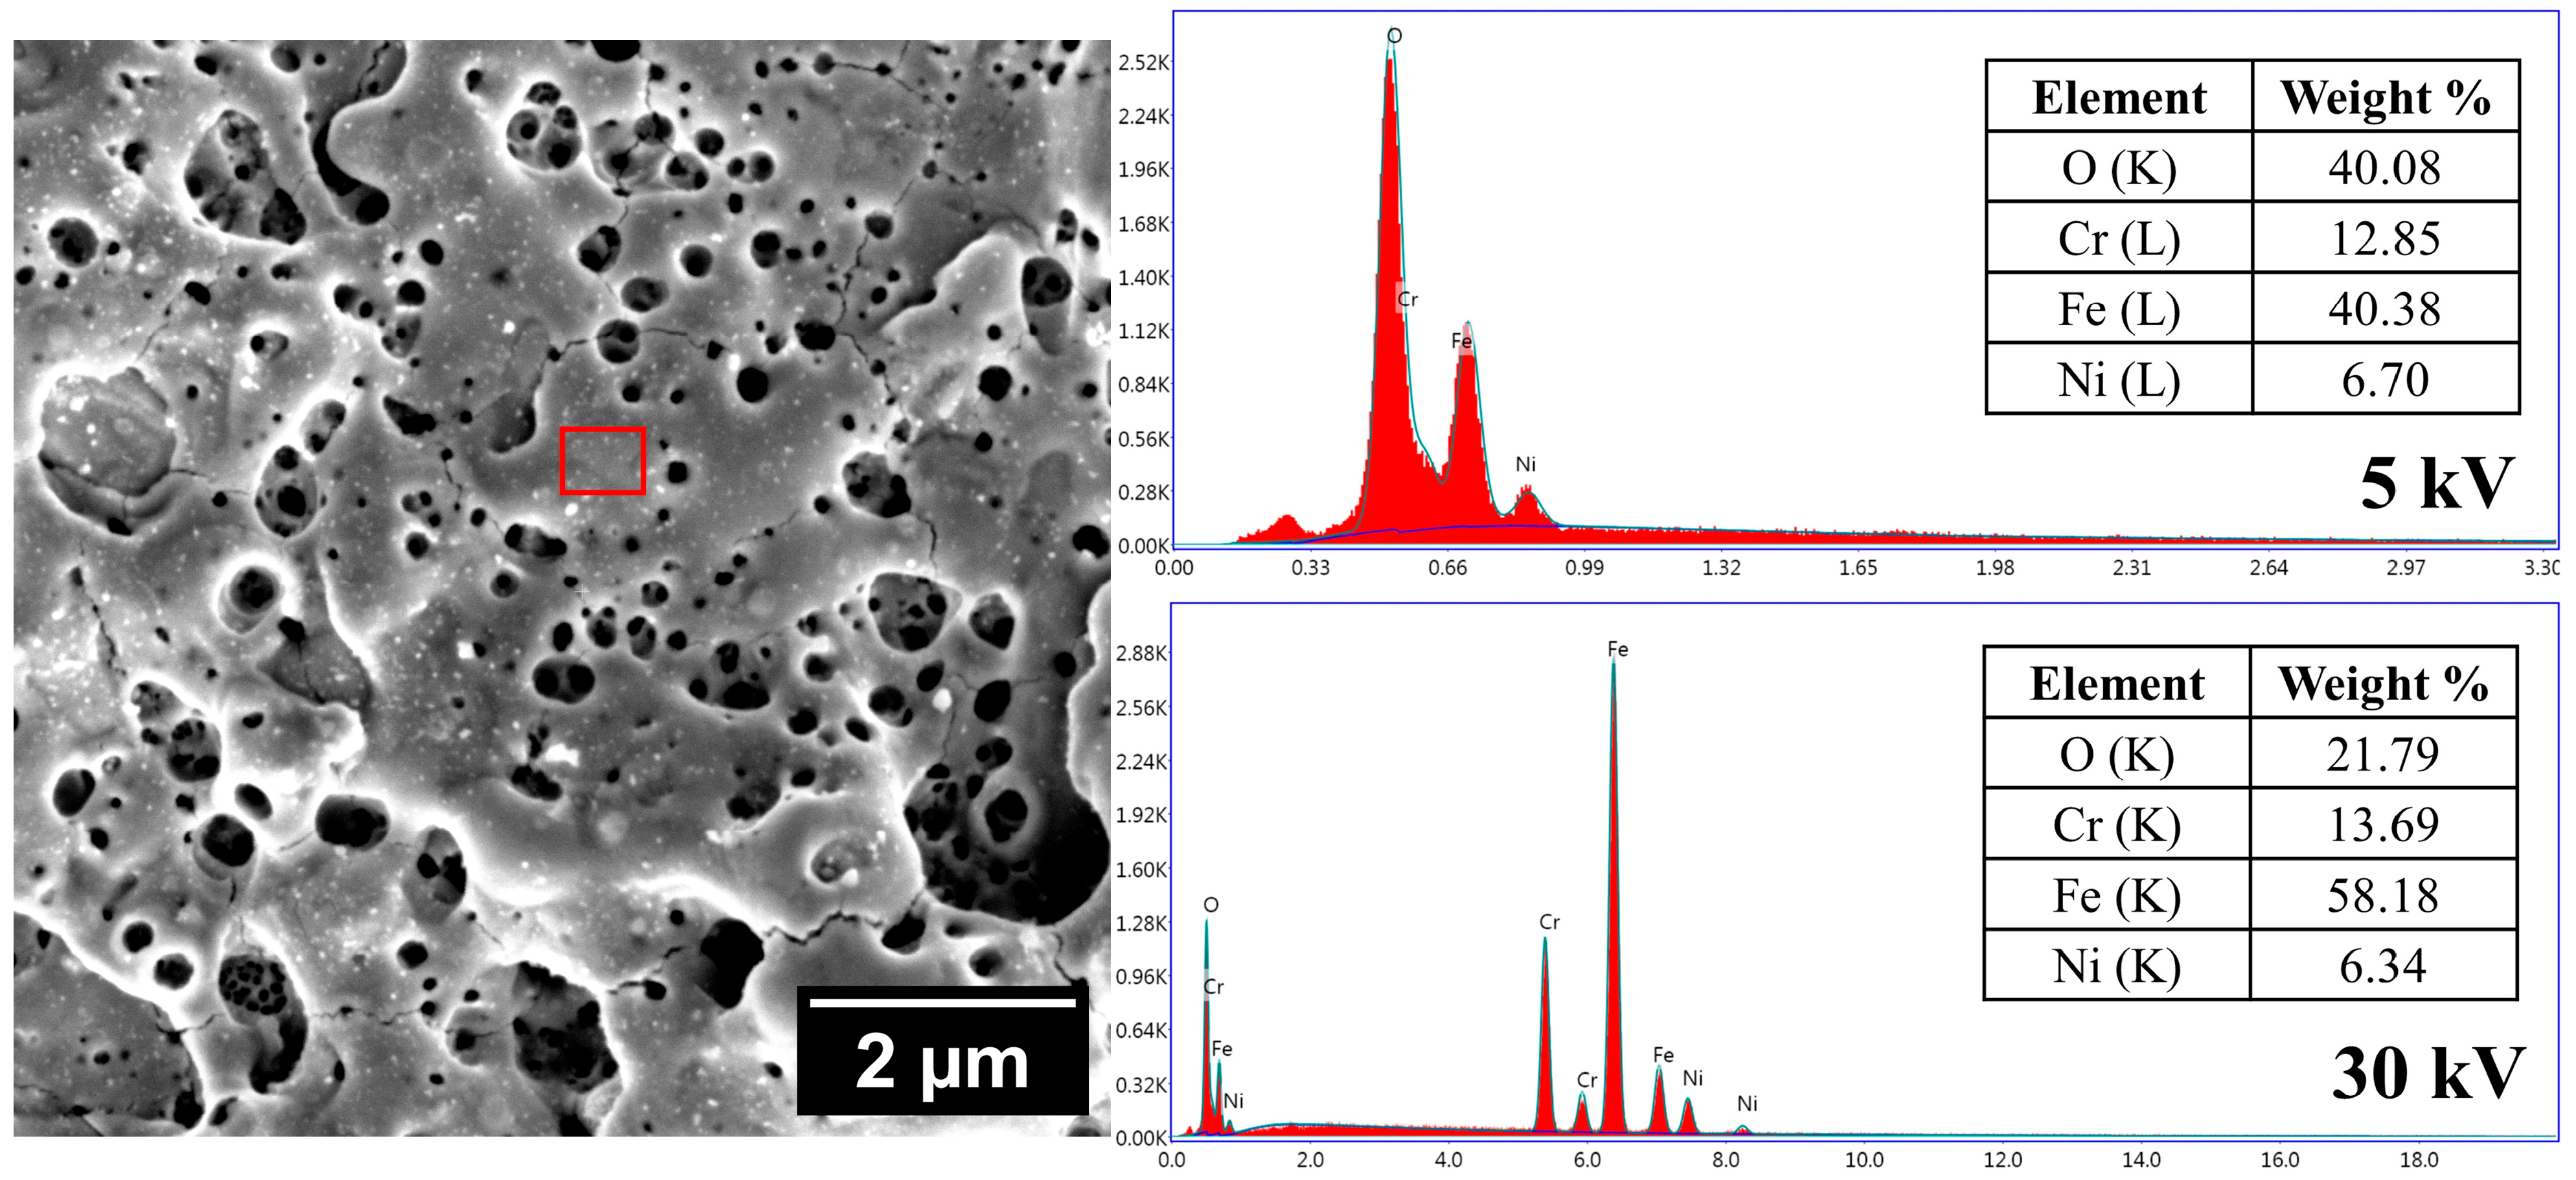
To further characterize the surface condition of the LSPwC specimen, SEM imaging coupled with EDS analysis was performed on the laser-ablated region. As shown in Figure 5, the LSPwC-treated surface exhibits a highly textured morphology with numerous pores. EDS analyses conducted at an accelerating voltage of 5 and 30 kV reveal surface enrichment in Fe and O, indicative of the formation of an iron-rich oxide layer following surface treatment. The higher oxygen content observed at 5 kV reflects increased surface sensitivity and possible overestimation associated with low-energy L-line analysis, whereas the lower oxygen contribution at 30 kV suggests that oxidation is largely confined to the near-surface region. The presence of an iron-rich oxide layer and surface porosity may interfere with repassivation and could contribute to reduced corrosion resistance in the LSPwC specimens.
Figure 5.
SEM SE micrograph of 304L stainless steel after LSPwC processing, with EDS-determined weight percent chemical composition of the ablated surface acquired at 5 and 30 kV from the region indicated by the red box.
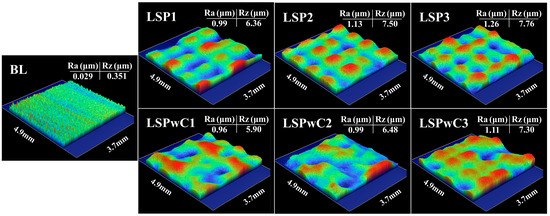
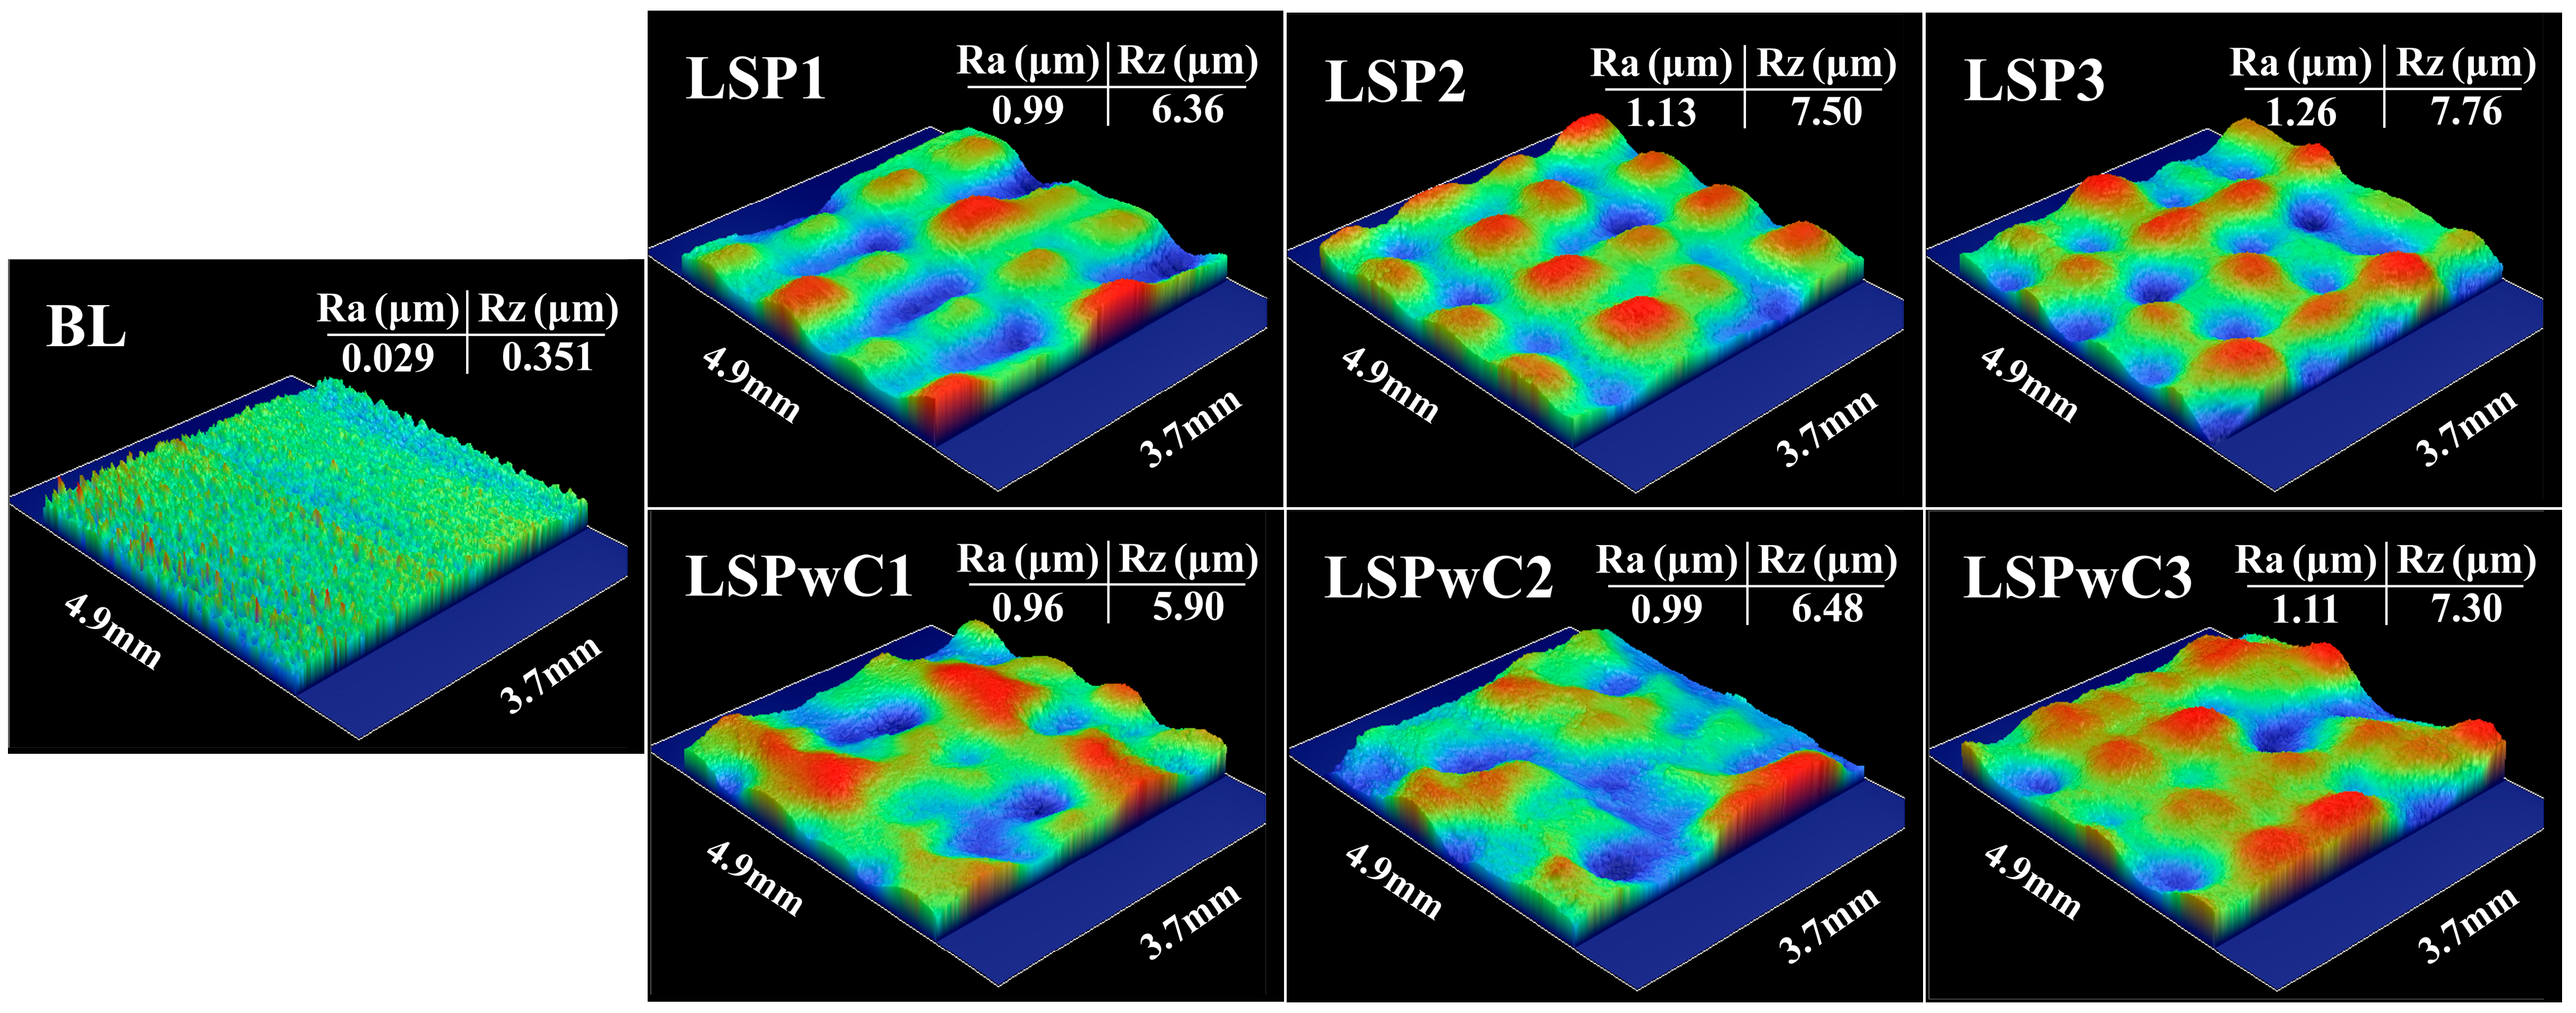
Figure 6 presents the 3D surface profiles of the BL specimens before and after LSP treatment. Surface roughness measurements revealed a notable increase in both roughness average (Ra) and average maximum height (Rz) compared to the untreated baseline. The BL specimen exhibited a smooth surface with minimal topographic variation, consistent with standard mechanical polishing. In contrast, all LSP-treated conditions showed elevated roughness values that increased slightly with pulse energy. This increase is attributed to localized plastic deformation and surface uplift caused by high-intensity shockwave impacts during peening. Similarly, the LSPwC surfaces exhibited roughness values comparable to, but slightly lower than, those of the LSP conditions. This difference is likely attributed to localized thermal effects associated with surface ablation during direct laser–material interaction.
Figure 6.
3D surface profile with roughness average (Ra) and average max height (Rz) after LSP and LSP without protective coating.
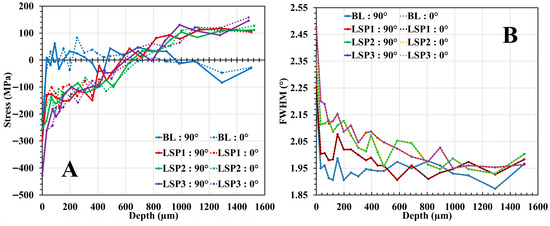
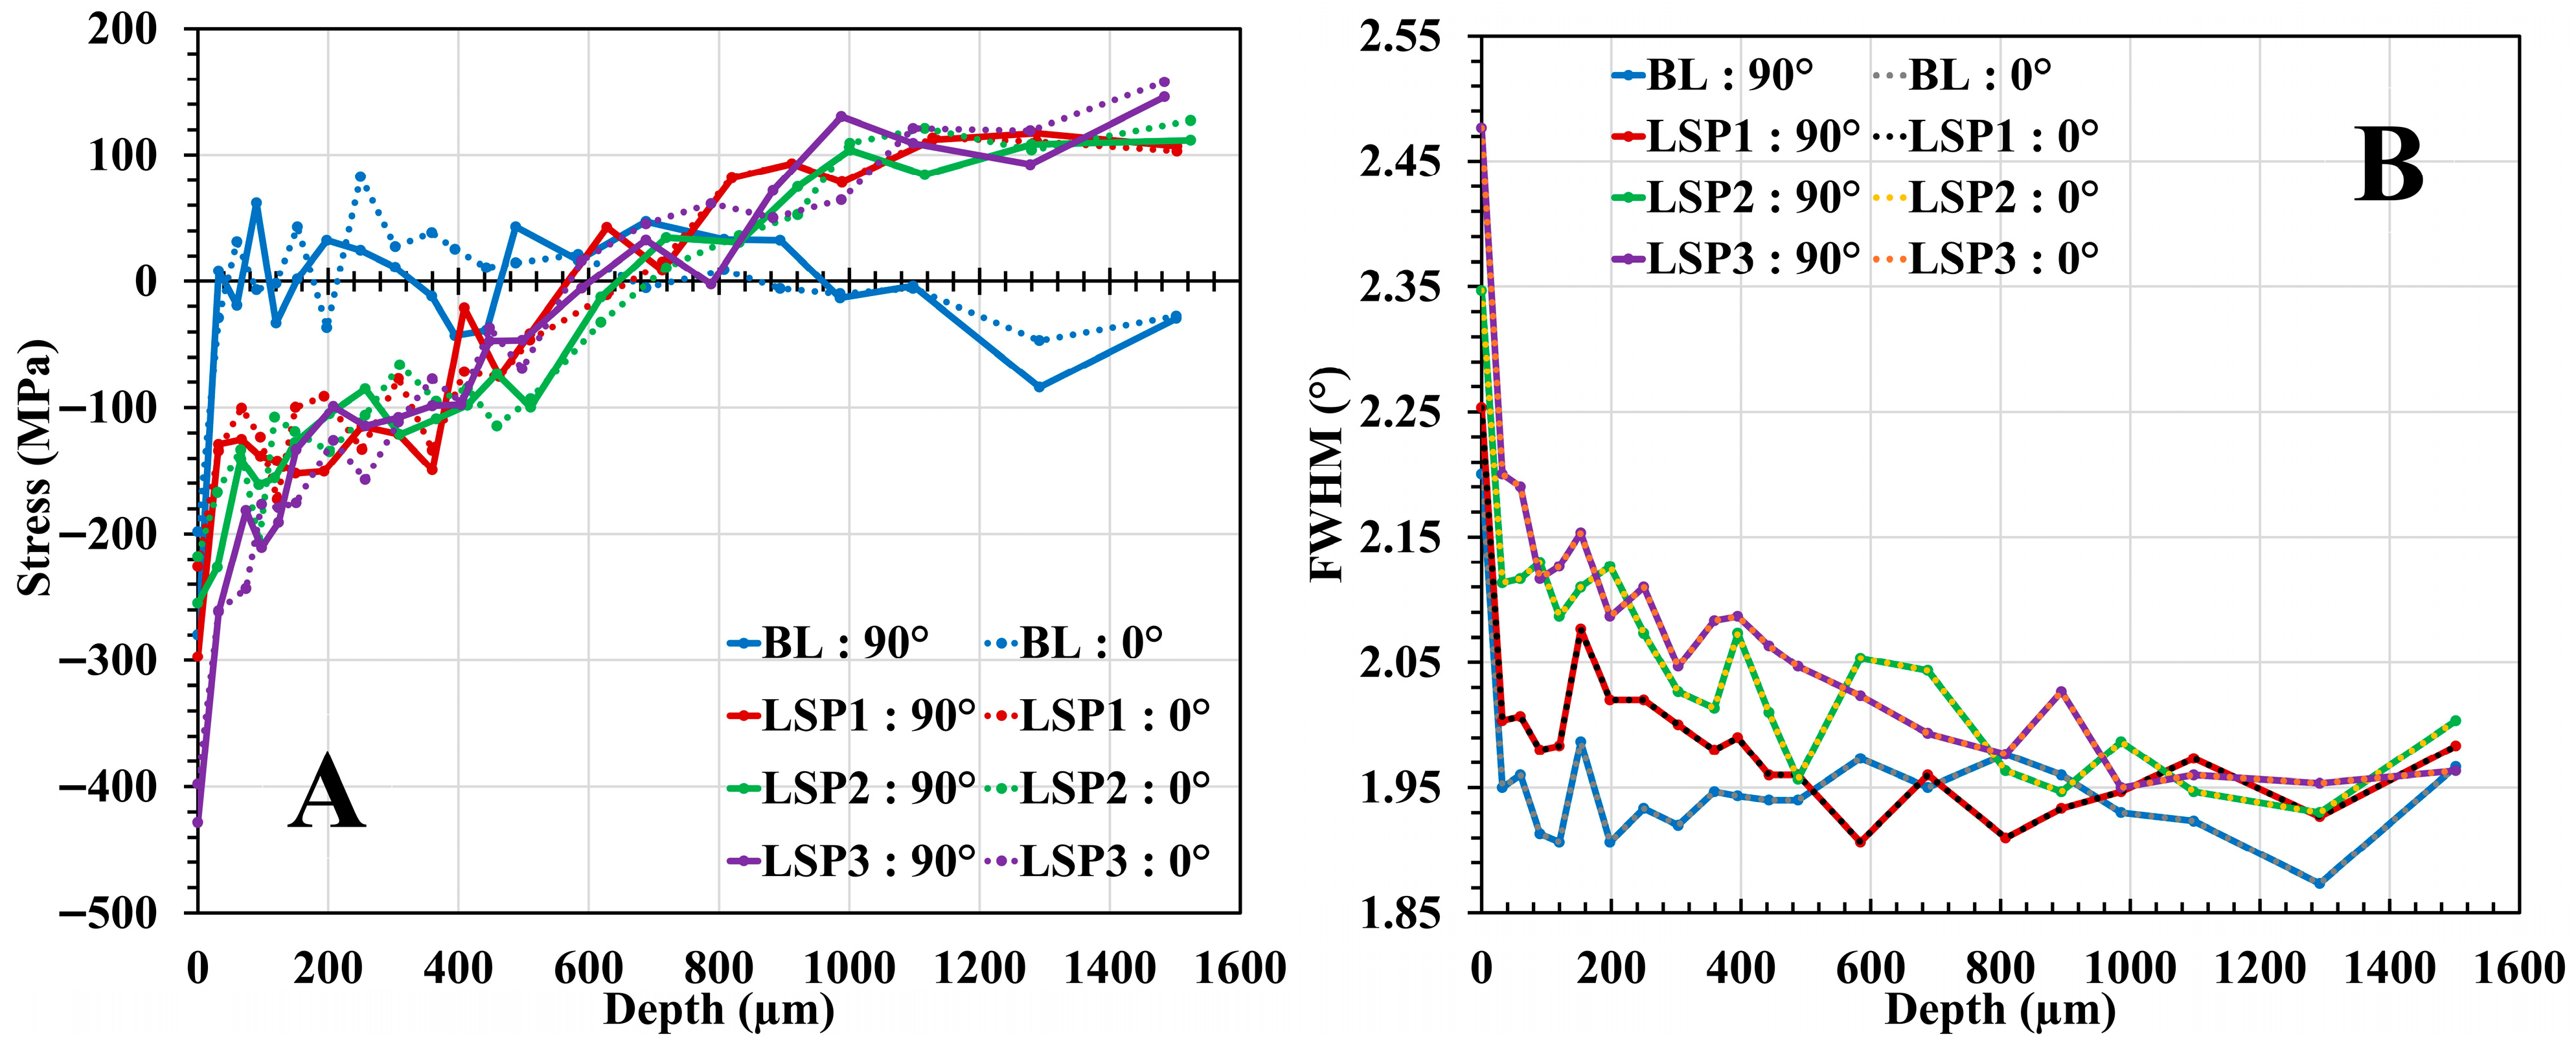
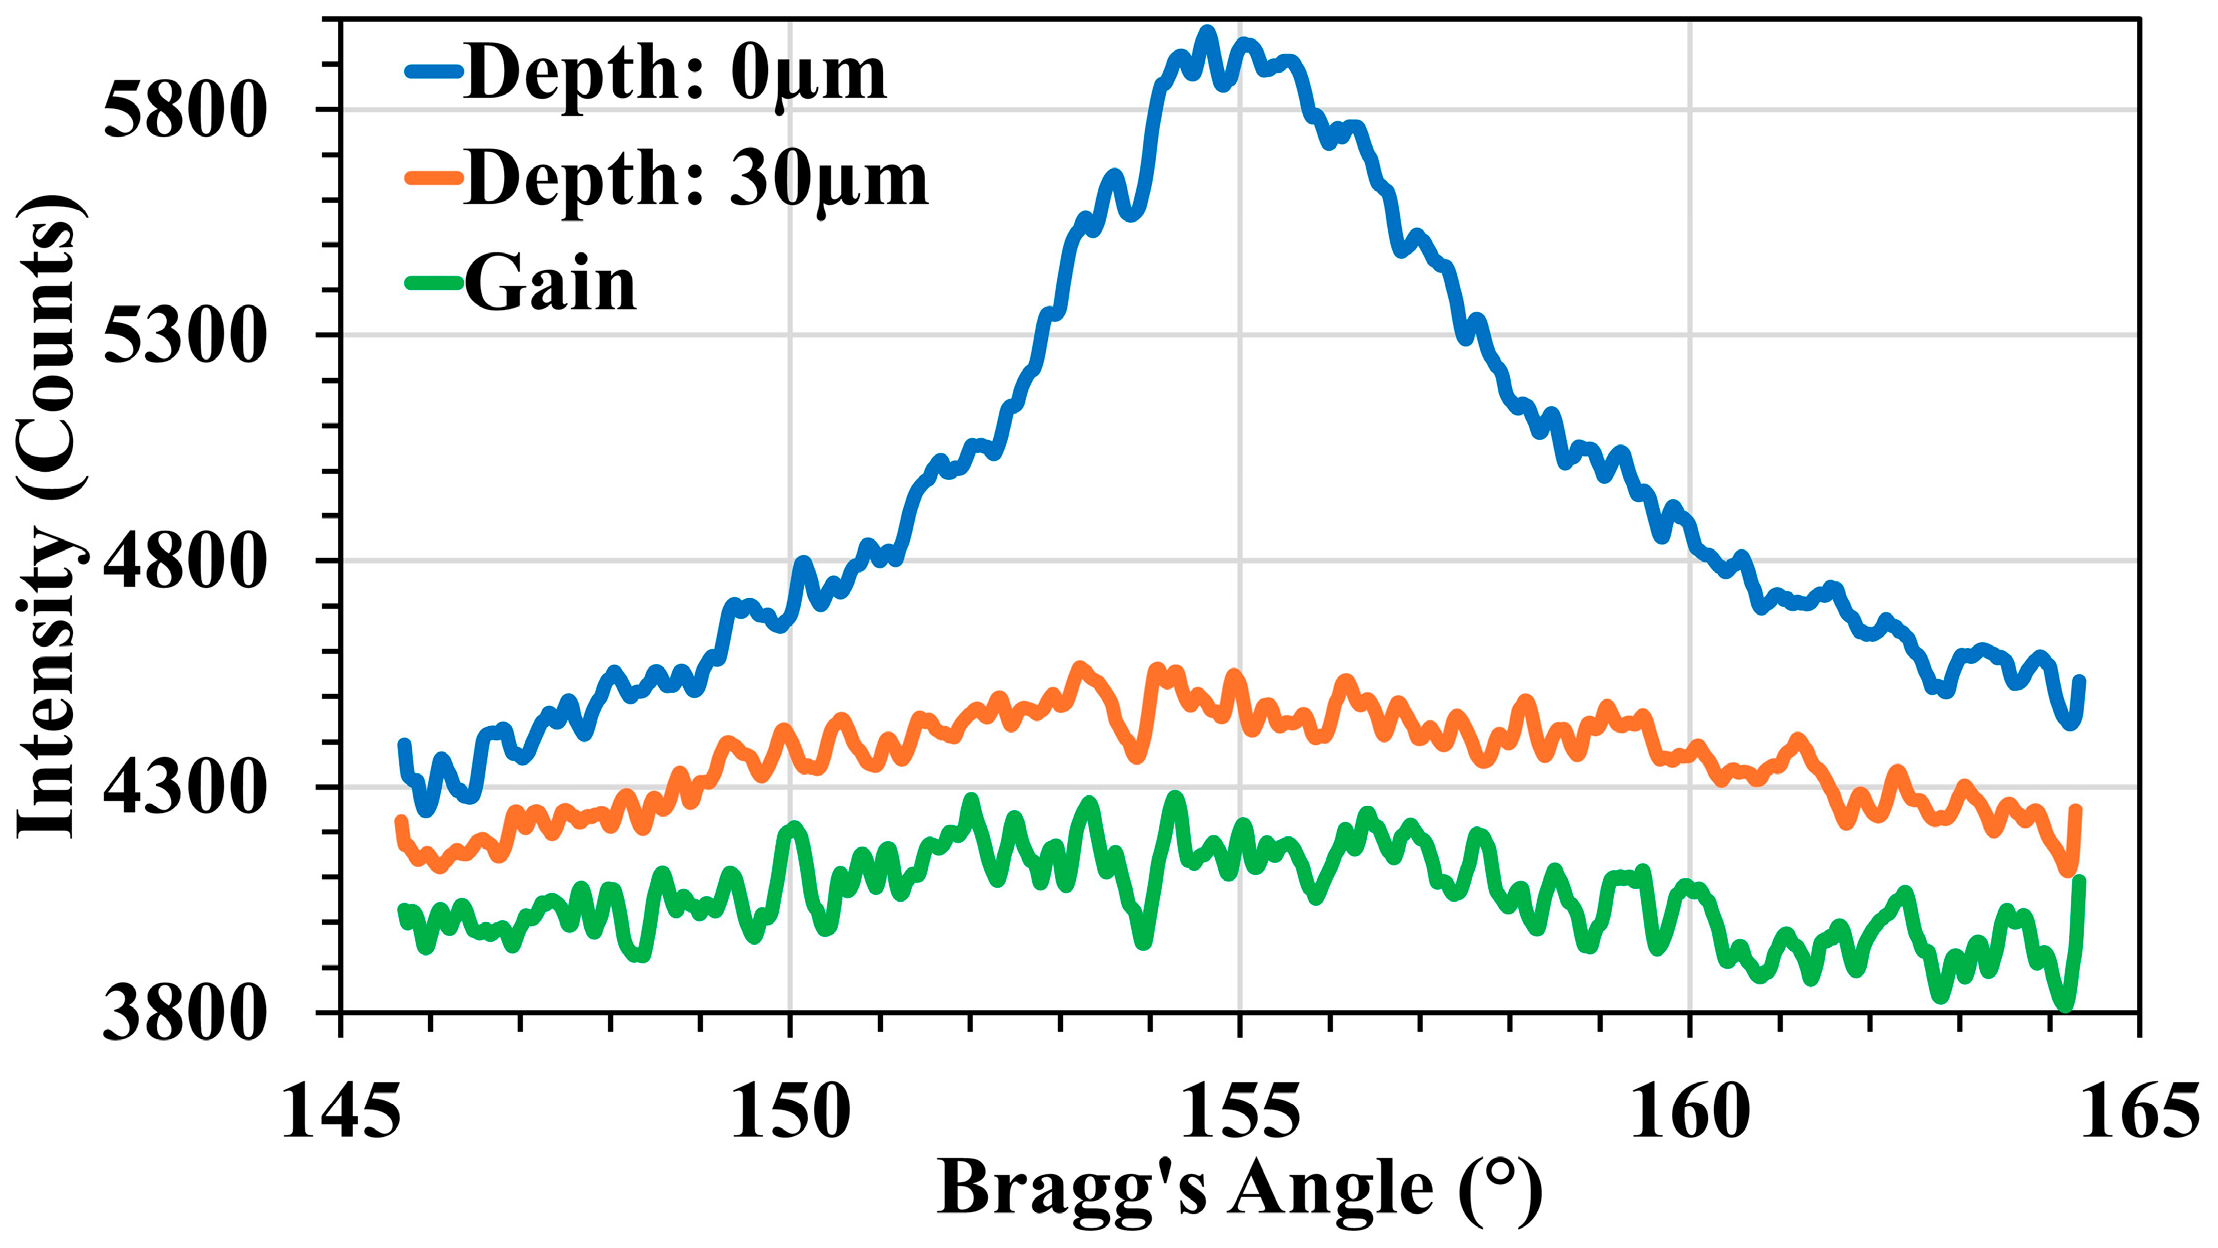
As shown in Table 6, surface residual stress measurements obtained by LXRD indicated that all specimen conditions were in a compressive stress state, with the magnitude increasing with laser pulse energy. The BL condition exhibited low surface compression attributed to mechanical polishing, which rapidly relaxed to a near-zero state following removal of the top 30 μm by electropolishing. This near-neutral stress profile remained consistent throughout the measured depth in the BL specimen, as depicted in Figure 7A. In contrast, the LSP-treated specimens showed significantly higher compressive stresses and increased penetration depths with both parameters scaling with laser energy. The compressive stress gradually decreased with depth, reaching BL-level stresses at ~600 μm, before transitioning to a tensile stress regime (Figure 7A). This transition from near-surface compression to subsurface tension is characteristic of self-equilibrating residual stress fields produced by LSP. The plastically deformed surface layer is elastically constrained by the underlying material, requiring a compensating tensile region at depth to maintain mechanical equilibrium. Depth profiling of the martensitic phase was not feasible, as the low-intensity martensitic peak disappeared after the initial electrolytic polish (Figure 8). The weak martensitic signal further suggest that only a small fraction of the austenitic phase transformed to martensite overall.
Table 6.
Surface residual stress of as-polished BL specimens following LSP surface treatment.
Figure 7.
(A) Residual stress and (B) FWHM depth profiles of 304L stainless steel specimens treated with LSP at varying pulse energies (0 J, 1 J, 1.5 J, and 3 J).
Figure 8.
Martensite peak from LXRD disappears following EP.
FWHM analysis of the diffraction peaks provided insight into the plastic strain distribution induced by LSP and further supported the residual stress depth profiling results. The BL specimen exhibited narrow and consistent FWHM values throughout the measured depth, apart from slight broadening at the surface due to minor lattice distortion from mechanical polishing (Figure 7B). In contrast, the LSP-treated specimens exhibited elevated FWHM near the surface, with greater peak broadening observed at higher laser intensities. This increase is attributed to a higher dislocation density and localized lattice strain generated by shock peening. Similar to the residual stress profiles, FWHM values decreased progressively with depth, approaching baseline levels near 650 μm. These findings confirm that LSP introduces significant near-surface strain and dislocation structures that contribute to the observed compressive stress field.
3.2. Cyclic Polarization
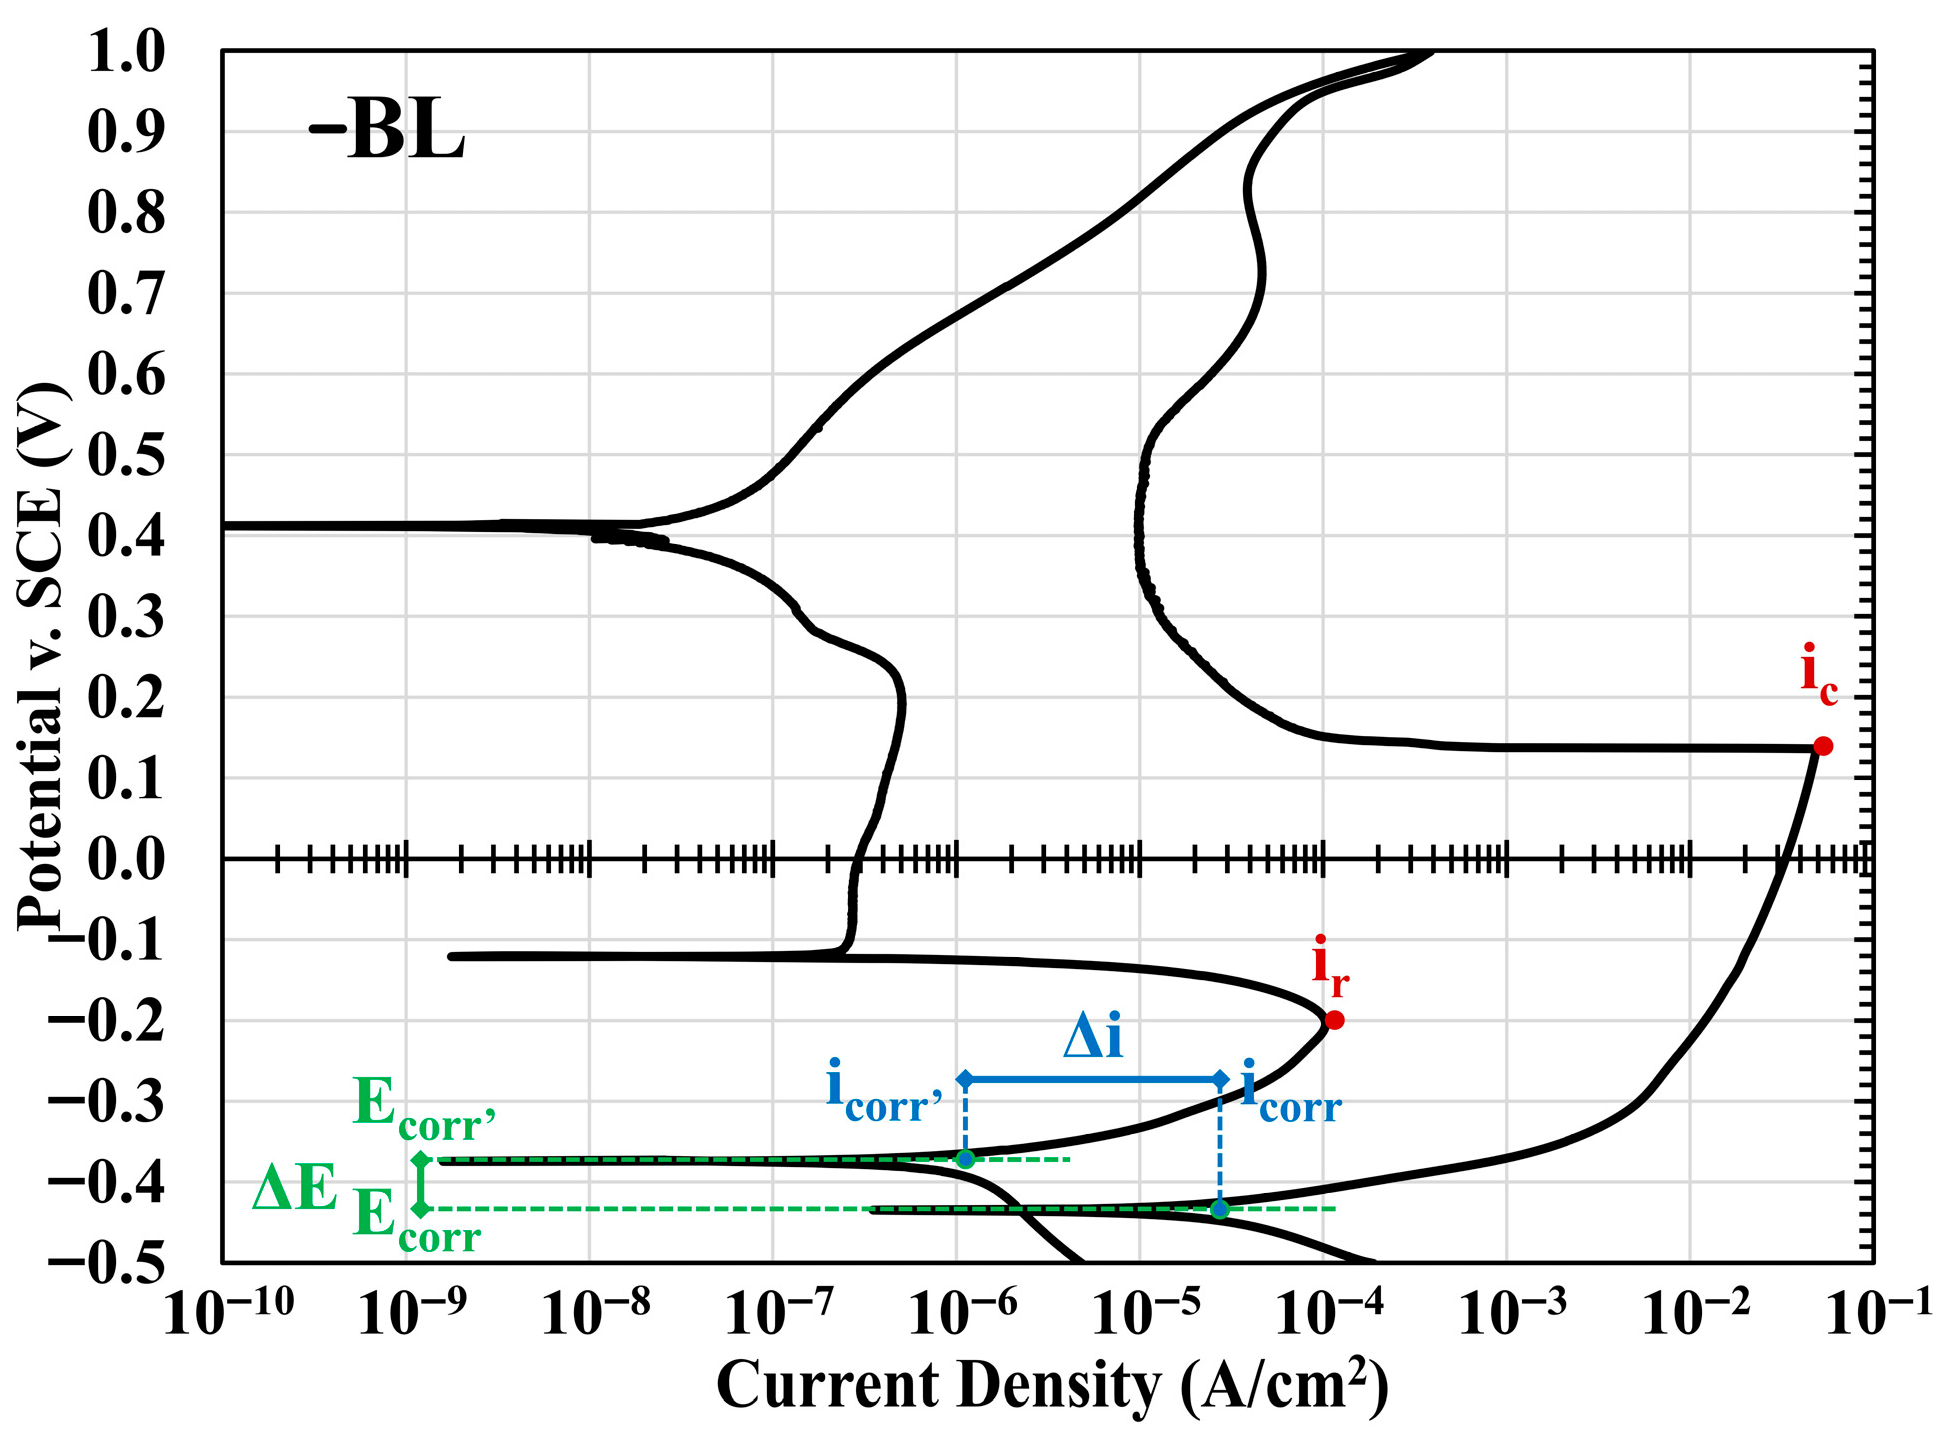
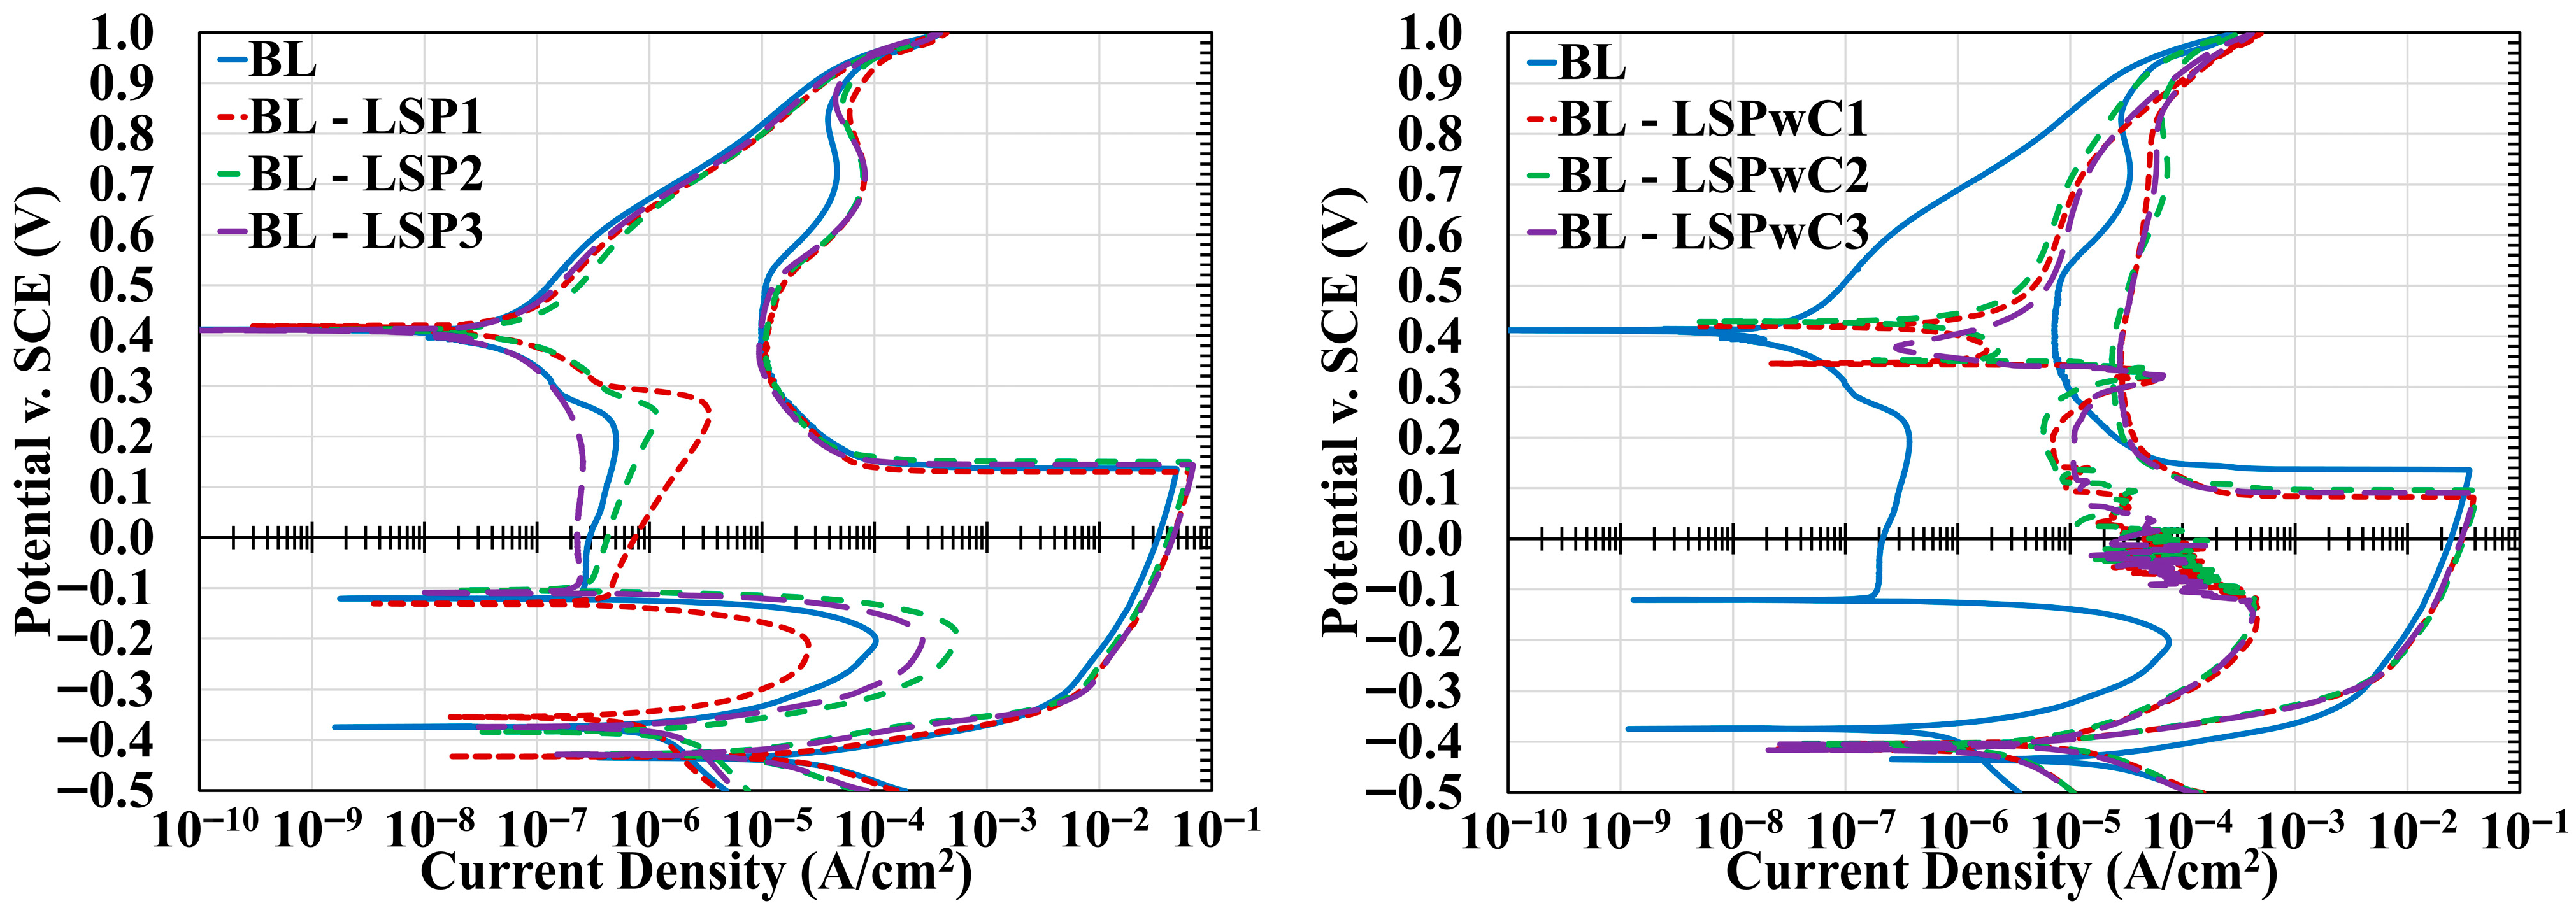
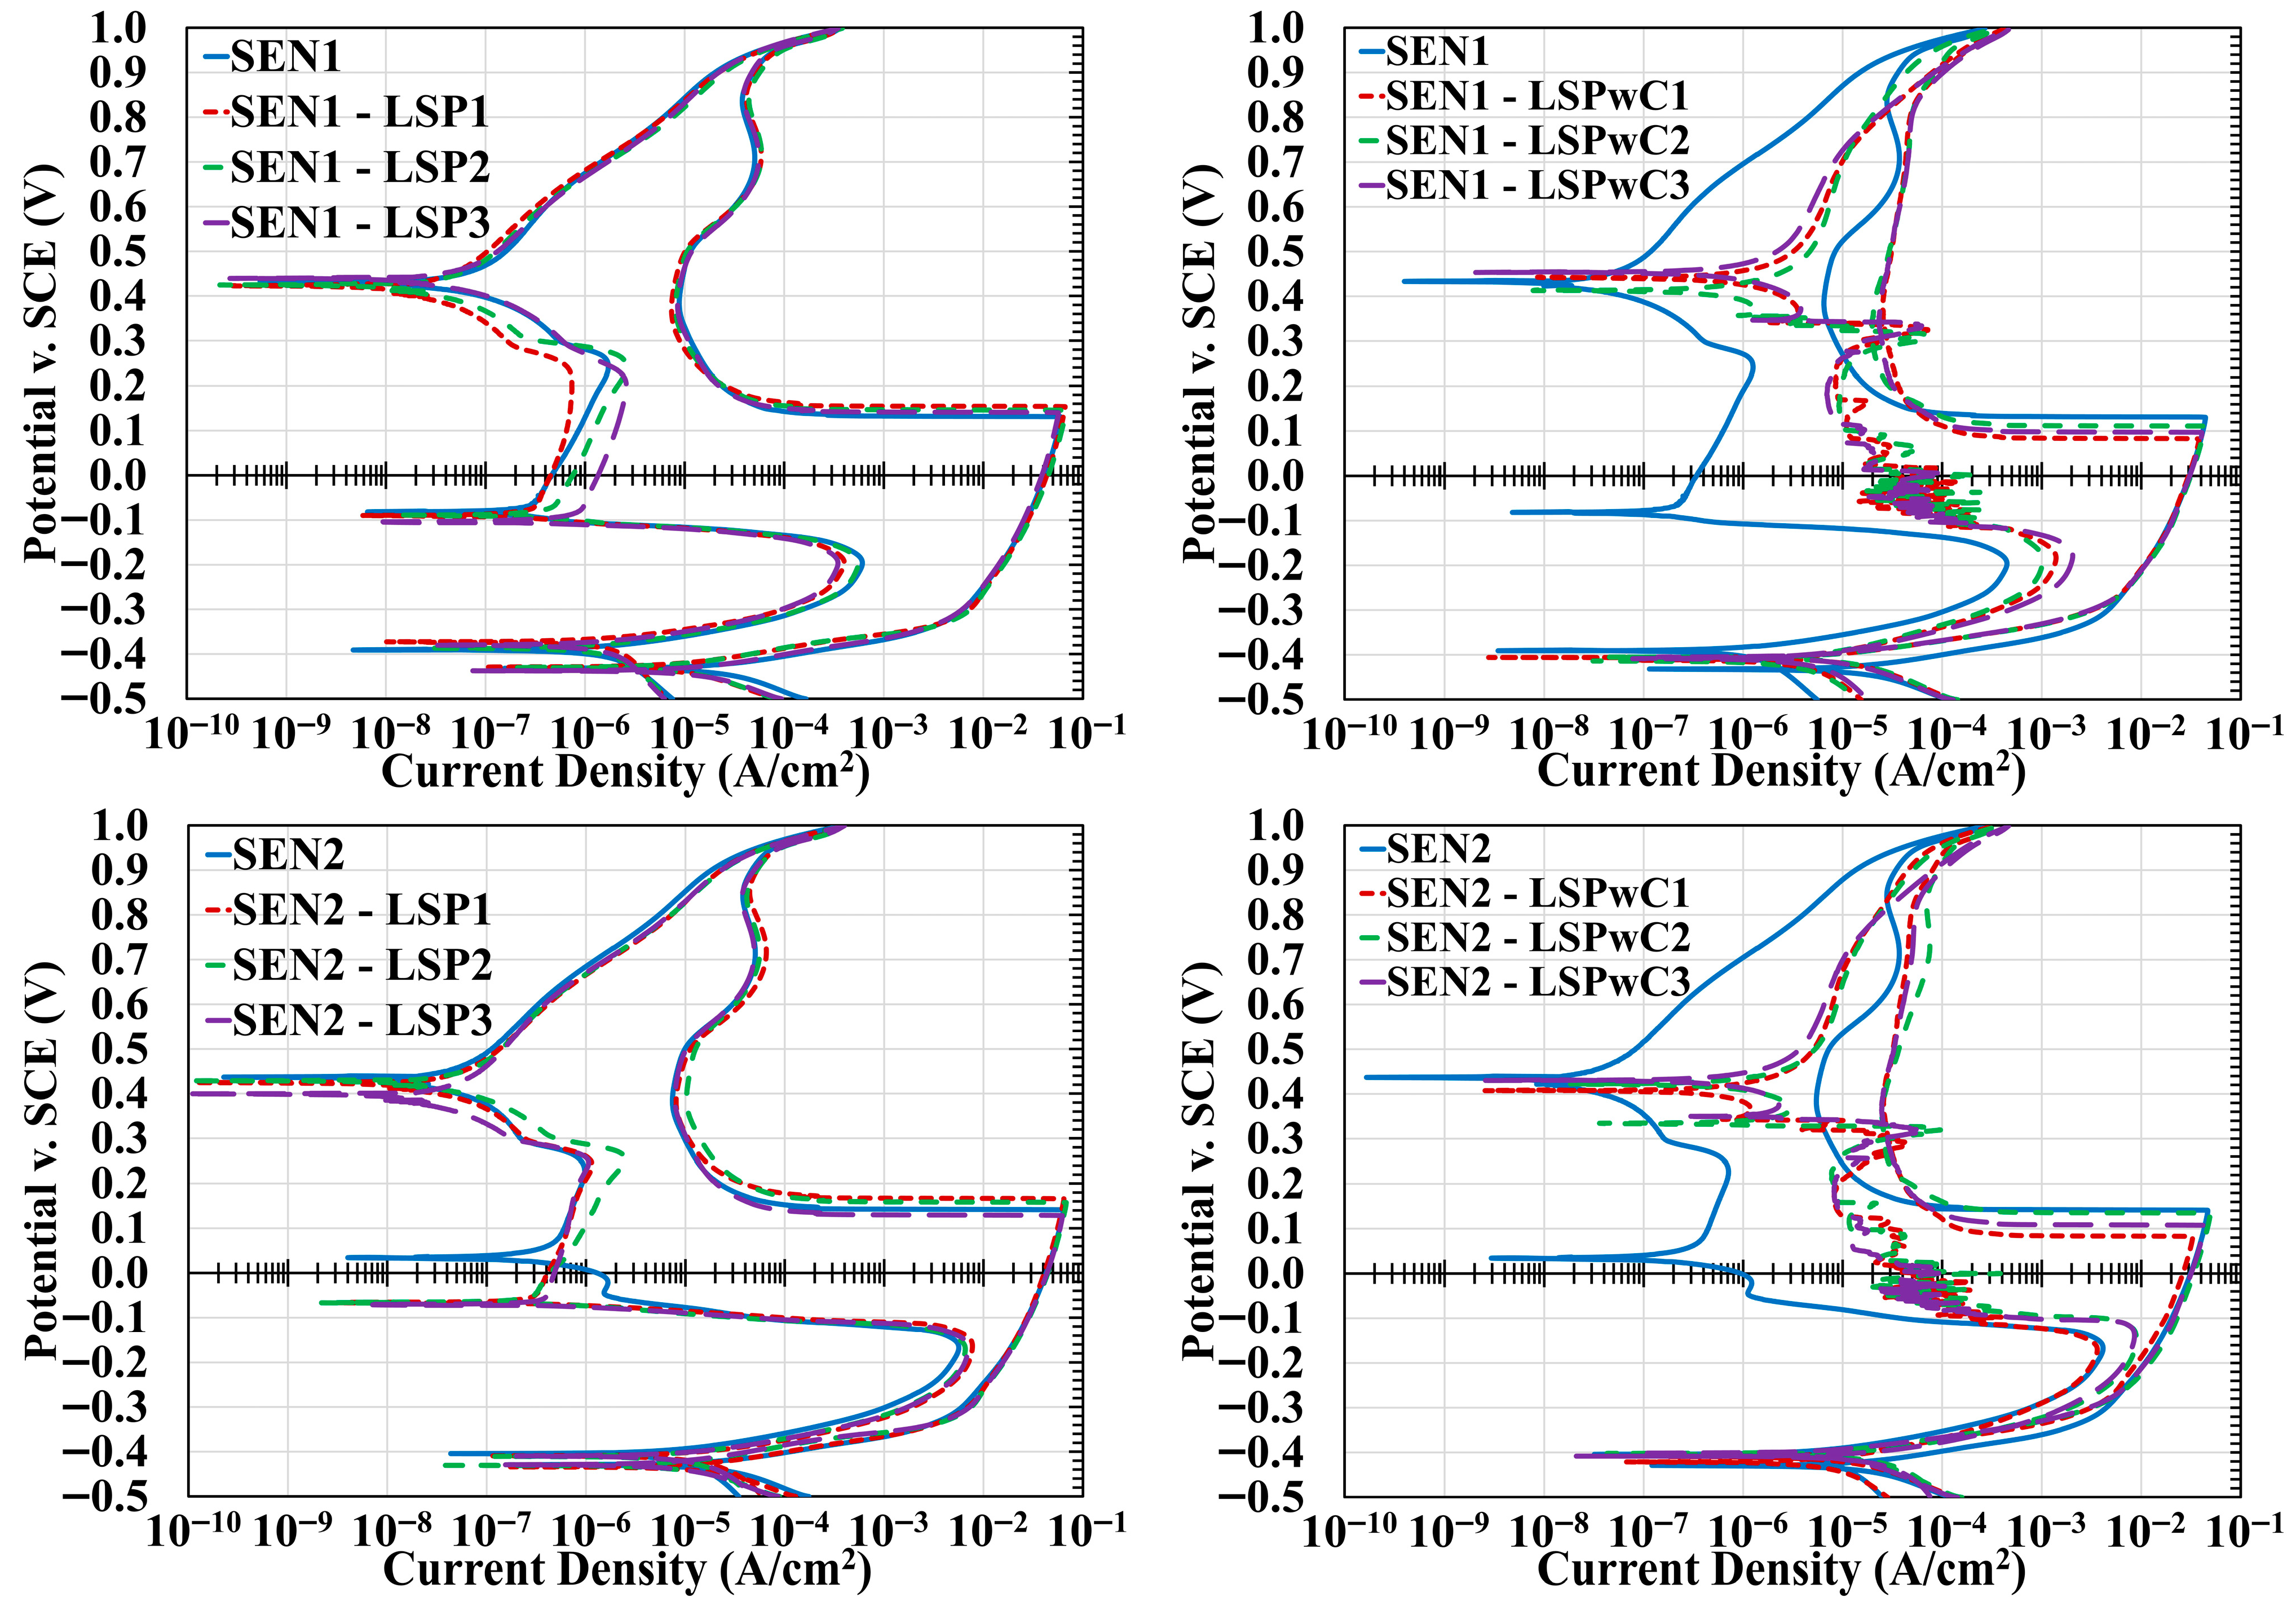
Cyclic potentiodynamic polarization tests were conducted in a 0.5 M H2SO4 + 0.05 M KSCN solution to assess the influence of laser shock peening (LSP), both with and without a sacrificial coating (LSPwC), on the corrosion behavior of sensitized 304L stainless steel. The specimen matrix included an as-polished baseline (BL) and two sensitized conditions: SEN1 (650 °C for 5 h) and SEN2 (650 °C for 24 h), each evaluated in untreated, LSP-treated, and LSPwC-treated states across varying laser intensities. Figure 9 presents a schematic cyclic polarization curve highlighting the key electrochemical parameters. As shown in Figures 10 and 12, all specimens exhibited typical active-passive behavior, characterized by anodic activation, a passive plateau, and transpassive breakdown. Key electrochemical parameters extracted from the tests are summarized in Table 7. Figure 11 presents representative SEM images showing surface degradation for the BL, SEN1, and SEN2 conditions following polarization testing.
Figure 9.
Representative cyclic polarization curve for 304L stainless steel exposed to 0.5 M H2SO4 + 0.05 M KSCN with key electrochemical parameters labeled.
Table 7.
Electrochemical data from cyclic polarization curves for 304L stainless steel specimens (BL, SEN1, and SEN2) subjected to LSP and LSPwC, tested in 0.5 M H2SO4 + 0.05 M KSCN.
To quantify the effects of sensitization and surface treatment, the degree of sensitization (%DOS) was calculated for each specimen condition. The sulfuric acid and thiocyanate environment is highly sensitive to changes in passive film integrity, making it well-suited for evaluating corrosion susceptibility in austenitic stainless steels. The %DOS is defined as the ratio of the reactivation current density (ir) to the critical current density (iC), as given in Equation (1). As illustrated in Figure 9, iC corresponds to the maximum current density measured during the forward scan prior to the onset of passivation, while ir is taken as the peak current density observed during the reverse scan following passivation. A lower ir relative to iC indicates a more stable passive film, as reactivation during the reverse scan is more effectively suppressed. Accordingly, lower %DOS values correspond to improved passivity and reduced susceptibility to intergranular corrosion (IGC). As a reference, %DOS values are commonly interpreted in four ranges: values below 1% indicate negligible susceptibility; 1–5% reflects slight susceptibility; 5–30% indicates moderate susceptibility; and values above 30% correspond to severe susceptibility.
This study confirms that %DOS varied significantly across the untreated specimen conditions, increasing with longer sensitization times (Figure 10). The BL specimen exhibited a low %DOS of 0.21%, indicating minimal susceptibility to IGC and a stable passive film. Post-experimental SEM analysis (Figure 11A) showed uniform surface corrosion with a step-like topography and minimal pitting, consistent with effective passivation. After sensitization at 650 °C for 5 h, the SEN1 specimen exhibited a %DOS of 1.01%, reflecting slight susceptibility due to localized chromium depletion from carbide precipitation. SEM images (Figure 11B) revealed features consistent with partial sensitization, including a mixture of step-like regions, shallow pits, and early trenching at grain boundaries. Extending the exposure to 24 h further increased the %DOS to 8.86%, indicating moderate IGC susceptibility and greater passive film degradation. The SEN2 surface (Figure 11C) exhibited more pronounced intergranular attack, deeper trenches, and increased pitting. These observations align with the expected progression of chromium carbide formation and chromium depletion at grain boundaries during prolonged sensitization heat treatment.
Figure 10.
Cyclic polarization curves for 304L stainless steel following sensitization heat treatment (0 h, 5 h, 24 h), exposed to 0.5 M H2SO4 + 0.05 M KSCN.
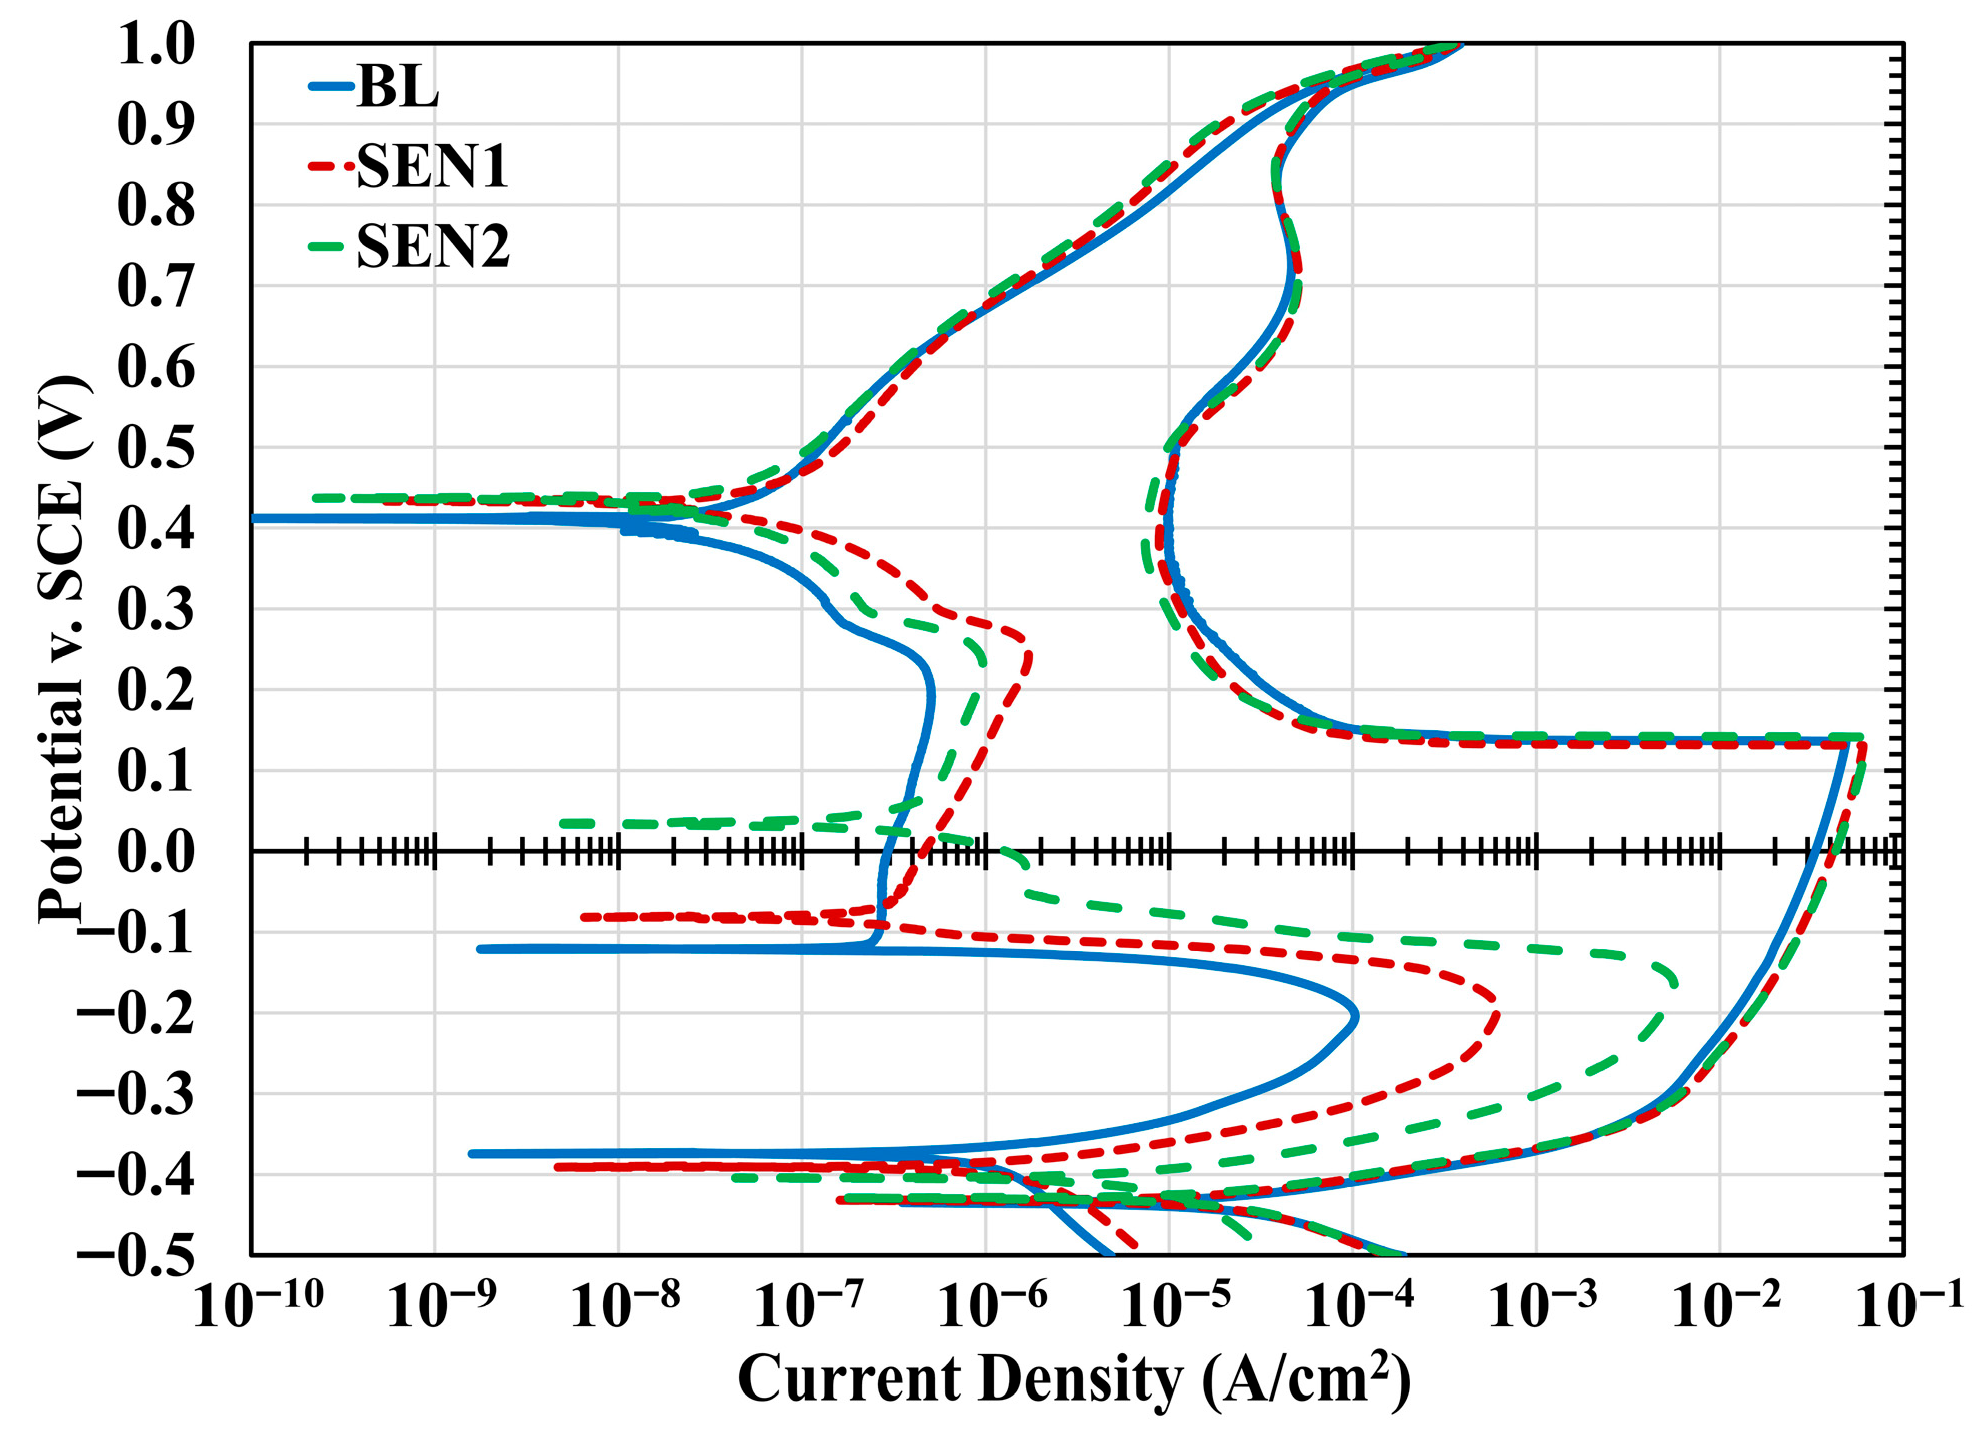
Figure 11.
SEM SE micrographs of as-polished 304L stainless steel in three conditions: (A) BL; baseline, (B) SEN1; sensitized for 5 h, and (C) SEN2; sensitized for 24 h after electrochemical testing.
Compared to their untreated counterparts, the LSP-treated specimens exhibited measurable changes in corrosion response across both baseline and sensitized conditions (Figure 12). For the BL specimens, low-energy LSP (LSP1) reduced %DOS from 0.21% to 0.04%, indicating improved passivation likely associated with the introduction of compressive residual stresses and possible modifications to lattice strain and dislocation substructure, as inferred from XRD peak broadening. At moderate (LSP2) and high (LSP3) energy levels, %DOS increased slightly to 0.87% and 0.39%, respectively, suggesting diminishing returns or minor disruption to film stability, potentially linked to increased surface roughness and dislocation density. Despite these increases, both conditions remained below the 1% threshold, indicating negligible susceptibility. In contrast, BL specimens treated without a protective coating (LSPwC) exhibited higher %DOS values exceeding 1%, placing them in the slightly susceptible range. This degradation is likely due to the surface oxidation and ablation introduced from laser exposure, which may compromise passive film integrity and promote localized corrosion.
Figure 12.
Cyclic polarization curves for 304L stainless steel specimens (BL, SEN1, and SEN2) subjected to LSP and LSPwC, exposed to 0.5 M H2SO4 + 0.05 M KSCN.
For the SEN1 condition, LSP improved corrosion resistance relative to the untreated specimen (Figure 12). LSP1 and LSP3 reduced %DOS to 0.61%, while LSP2 yielded a slightly higher value of 0.82%, suggesting that LSP partially mitigated the sensitization effects through the introduction of compressive residual stress and possibly enhanced chromium mobility toward the surface. This may have helped counteract chromium depletion at grain boundaries caused by carbide precipitation. In contrast, the LSPwC specimens exhibited increased %DOS values following surface treatment, though susceptibility remained low in all cases. The higher %DOS suggests that macrostructural defects, such as the formation of unstable iron oxides, played a dominant role in the corrosion behavior. The oxide layer likely compounded the weakened passivity by further localizing the electrochemical attack leading to increased pitting and IGC.
In the more heavily sensitized SEN2 condition, LSP treatment slightly worsened corrosion performance, with %DOS values increasing to 11.99% (LSP1), 9.66% (LSP2), and 11.32% (LSP3). These results indicate that under the current processing parameters, LSP is ineffective at restoring passivity once extensive grain boundary chromium depletion has occurred. LSPwC-treated specimens performed even worse, further supporting the hypothesis that surface oxidation caused by unprotected laser exposure significantly degrades corrosion resistance.
Overall, trends in %DOS demonstrate that while LSP can modestly improve passivity in mildly sensitized stainless steel, its effectiveness diminishes under moderate sensitization, particularly when no protective coating is used. To further evaluate corrosion performance, changes in corrosion potential (ΔECORR) and corrosion current density (ΔiCORR) were analyzed to assess the material’s corrosion tendency and passive film stability across treatment conditions.
ΔECORR, defined as the difference between the corrosion potentials obtained during the forward (ECORR) and reverse (ECORR′) scans, reflects the stability of the passive film, with more positive ΔECORR values suggesting better repassivation behavior. Similarly, ΔiCORR represents the change in corrosion current density between the forward (iCORR) and reverse (iCORR′) scans, where a negative ΔiCORR signifies reduced anodic activity due to a stable passivity, while a positive ΔiCORR denotes increased active corrosion resulting from limited repassivation. To determine the corrosion current density, Tafel extrapolation of the anodic and cathodic branches near the corrosion potential was performed. The fitting window was selected to ensure linear behavior on a semi-logarithmic scale with a goodness-of-fit (R2) between 1.0–3.0.
As shown in Table 7, the BL condition exhibited the most favorable electrochemical response, with a ΔECORR of +60.6 mV and a ΔiCORR of −25.92 μA/cm2, indicating strong repassivation and a stable passive film. In contrast, the sensitized specimens exhibited progressively poorer performance with increasing thermal exposure. The SEN1 specimen showed a lower ΔECORR (+41.1 mV) and a less negative ΔiCORR (−21.52 μA/cm2), while the SEN2 specimen demonstrated a further decline in corrosion performance, with a ΔECORR of +24.8 mV and a ΔiCORR of −10.43 μA/cm2. These results confirm the detrimental effect of chromium carbide precipitation on passive film stability, arising from chromium depletion at grain boundaries during sensitization.
For the LSP-treated surfaces, the results show improvements in both ΔECORR and ΔiCORR for the BL and SEN1 conditions. In the BL specimens, the LSP1 treatment produced the most beneficial response, yielding a ΔECORR of +78.1 mV and a ΔiCORR of −22.64 μA/cm2, indicative of enhanced repassivation behavior. This improvement is attributed to the introduction of compressive residual stress, which promotes passive film stability. However, at higher pulse energies, corrosion performance declined, as reflected by lower ΔECORR values and less negative ΔiCORR values. This reduction in stability is likely associated with increased surface roughness, which can disrupt passive film continuity.
In the SEN1 condition, LSP treatment remained advantageous across all energy levels, with a modest increase in ΔECORR, suggesting that LSP mitigated the adverse effects of chromium depletion by promoting passive film recovery. Conversely, in the SEN2 condition, passivation weakened following LSP, implying that in severely sensitized 304L stainless steel, the extent of chromium depletion from the carbide precipitation may exceed the restorative capacity of LSP. Further optimization of LSP parameters may be necessary to achieve corrosion improvement under such conditions.
Compared with their LSP-treated counterparts, the LSPwC specimens consistently exhibited inferior corrosion performance across all base conditions. The slightly negative ΔECORR values indicate that surface oxidation hindered the formation of a stable passive film. Moreover, the ΔiCORR values remained small and less negative, suggesting persistent anodic activity through an unprotective Fe-oxide layer that promotes localized corrosion. These findings underscore the detrimental effects of uncoated laser peening and highlight the essential role of a sacrificial confining layer in maintaining surface integrity and corrosion resistance during LSP processing.
Although parameters such as %DOS ΔECORR, and ΔiCORR offer valuable insight into a material’s passive behavior, they do not directly quantify its degradation rate in a defined environment. To address this limitation, the corrosion rate (CR) was calculated using Faraday’s law, as shown in Equation (2), based on the measured iCORR values and the following constants: a corrosion rate constant (K) of 3272 cm, an equivalent weight (EW) of 25.12, a density (d) of 7.87 g/cm3, and a surface area (A) of 1.00 cm2 [41].
For the BL condition, the untreated specimen exhibited a CR of 0.718 mmpy. This value decreased substantially following LSP, with BL-LSP2 and BL-LSP3 showing the lowest rates at 0.195 and 0.218 mmpy, respectively. The improvement is attributed to the introduction of compressive residual stress and increased dislocation density, both of which likely contributed to reduced alloy dissolution. Similar reductions were observed in the SEN1 and SEN2 conditions after LSP treatment, demonstrating that the technique remains effective even in sensitized microstructures. LSPwC-treated specimens also exhibited lower CR values across all base conditions; however, the similar rates suggest that this effect may be a result of the laser-induced surface oxide layer that temporarily limits electrolyte access.
It is important to distinguish between general corrosion behavior and susceptibility to localized corrosion. Corrosion rates derived from polarization measurements reflect the kinetics of uniform metal dissolution, whereas %DOS is specifically associated with susceptibility to localized corrosion. Consequently, a reduction in corrosion rate does not necessarily imply improved resistance to localized attacks or enhanced passive film stability.
Overall, these results indicate that LSP enhances the resistance of 304L stainless steel to uniform corrosion, consistent with improved surface stability under the conditions investigated. However, its effectiveness in mitigating localized corrosion remains limited under heavily sensitized conditions. This behavior highlights the governing role of chromium depletion at grain boundaries in controlling sensitization, which cannot be fully offset by LSP-induced surface modifications and compressive residual stress within the present processing window.
In the case of LSPwC, the observed decrease in corrosion rate concurrent with increased %DOS indicates that, while uniform corrosion kinetics may be reduced, susceptibility to localized corrosion is increased. This response is consistent with the presence of a Fe-rich oxide layer and surface porosity, which may impair passivity and increase the density of potential active corrosion sites.
4. Discussion
4.1. Effect of Laser Shock Peening on 304L Stainless Steel
Laser shock peening (LSP) was applied to 304L stainless steel under baseline (BL) and sensitized (SEN1, SEN2) conditions using varying pulse densities (LSP1, LSP2, LSP3). The objective was to assess whether LSP could enhance corrosion resistance by inducing compressive residual stress and improving passive film stability through increased dislocation density. A secondary aim was to determine whether higher peening intensities might promote deformation-induced martensite, which is known to compromise corrosion performance [28,42,43,44].
In austenitic stainless steels, severe plastic deformation (SPD) is typically accommodated by deformation twinning and dislocation slip, with the dominant mechanism governed by both stacking fault energy (SFE) and strain rate. For low-SFE alloys such as 304L, twinning is energetically favored due to the suppression of dislocation cross-slip. Chen et al. reported that martensitic transformation tends to occur at lower strain rates (10–103 s−1), while twinning dominates at rates above 104 s−1 [45]. Given that LSP induces strain rates on the order of 105 to 106 s−1, deformation twinning is expected to be the prevailing mechanism that occurs under these conditions [46].
XRD analysis supported this expectation, showing that LSP-treated specimens retained a predominantly austenitic microstructure with low-intensity martensitic peaks confined to the near-surface region. Similar peaks were observed in the as-polished untreated specimens, and in both cases, they disappeared after electropolishing. This suggests that the martensitic phase likely formed due to low strain-rate deformation during mechanical polishing, rather than as a result of the LSP surface treatment. These findings are consistent with previous studies reporting that LSP promotes twinning rather than martensitic transformation in low-SFE stainless steels [24,47,48]. However, it should be noted that direct characterization of deformation twinning was not conducted in this particular study, and thus these mechanisms are not explicitly confirmed here.
Residual stress and FWHM depth profiling confirmed that LSP introduced a substantial compressive stress field in the near-surface region of 304L stainless steel. In the BL specimens, only shallow compressive stress was observed from mechanical polishing, which was fully relieved after electrolytic removal of the top 30 μm. By contrast, LSP-treated specimens retained significant compressive stress to depths approaching 600 μm. Higher pulse densities resulted in greater stress magnitudes, deeper penetration, and increased dislocation density. This sustained subsurface compression is critical for improving corrosion resistance as it has been shown to help suppress crack initiation, reduce pit propagation, and decrease passive film degradation.
Several studies have confirmed that compressive residual stress, along with microstructural changes such as grain refinement, significantly enhances the corrosion resistance of austenitic stainless steels. Lu et al. demonstrated that LSP delayed crack initiation and reduced pit growth in 304 stainless steel by stabilizing the passive film through grain refinement and suppressing crack propagation via compressive stress [21,22]. Guan et al. similarly reported improved pitting resistance in 304L stainless steel, citing increased pitting potential, reduced metastable pit formation, and enhanced passive film quality attributed to the combined effects of surface compression and refined microstructure [24]. Brandal et al. observed a 65% increase in time-to-failure for LSP-treated 304 stainless steel in boiling MgCl2, attributing this improvement to high surface compression which increased the electron work function and strengthened passivation behavior [27].
The improvements reported in these studies are mirrored in the present investigation’s electrochemical results. For the mildly sensitized SEN1 condition, LSP significantly improved all measured metrics. The %DOS decreased to below 1%, indicating a transition from slight to negligible susceptibility to localized corrosion, while favorable shifts in ΔECORR suggested enhanced passive film stability and repassivation behavior. A corresponding reduction in corrosion rate further confirmed the effectiveness of LSP in reducing uniform metal dissolution kinetics, consistent with enhanced surface stability.
In contrast, the heavily sensitized SEN2 specimens showed limited recovery. %DOS and ΔiCORR remained elevated, indicating poor passivation and susceptibility to IGC. However, a modest decrease in corrosion rate suggests that LSP may still provide some surface protection against uniform corrosion. For the BL condition, LSP consistently reduced the uniform corrosion rate, but improvements in passivation metrics were less consistent, particularly at higher peening intensities. This could reflect tradeoffs associated with increased surface roughness or dislocation density.
Overall, these findings demonstrate that LSP is generally effective in mitigating corrosion in 304L stainless steel, especially under mild sensitization, though its capacity to restore passivity diminishes in more severely degraded microstructures. Further optimization of LSP parameters may be necessary to extend corrosion protection to more severely sensitized or structurally degraded materials.
4.2. Effect of Laser Shock Peening Without Protective Coating on 304L Stainless Steel
Laser shock peening without a protective coating (LSPwC) was applied to 304L stainless steel under baseline (BL) and sensitized (SEN1, SEN2) conditions using varying pulse densities (LSPwC1, LSPwC2, LSPwC3). This part of the study aimed to evaluate how the absence of a sacrificial overlay during LSP influences corrosion behavior by modifying surface chemistry. Specifically, it assessed whether the compressive stresses induced by LSPwC could still enhance corrosion resistance, despite the additional surface oxidation and potential thermal effects caused by direct laser–material interaction. To maintain consistency with the LSP-treated specimens, the processing strategy did not take advantage of the higher overlap efficiency typically achievable with LSPwC.
In this study, the LSPwC-treated specimens across all base conditions exhibited a consistent decline in corrosion performance compared to their LSP counterparts. This was evidenced by a shift toward more negative ΔECORR, more positive ΔiCORR, and higher %DOS values. The comparable roughness levels observed for LSP and LSPwC indicate that surface roughness alone cannot account for the reduced corrosion resistance observed in the LSPwC condition. Instead, these electrochemical trends suggest that direct laser exposure altered the surface composition by promoting Fe-oxide formation, which compromised passive film development. As a result, the corrosion resistance of 304L stainless steel was reduced, likely due to impaired passivation and increased susceptibility to localized corrosion.
XRD and EDS analysis provided insight into this behavior by confirming the presence of iron-oxides formed during LSPwC. Without a protective overlay, the stainless steel surface was directly exposed to plasma generated by the high-energy laser pulse, leading to localized ablation and thermal oxidation from reactions with nascent oxygen in the water confinement layer. This resulted in the formation of a greyish Fe-rich oxide layer on the treated surface. Similar oxidation has been reported in previous LSPwC studies on stainless steels [31,49]. While these oxides may provide temporary barrier effects, they are significantly less stable and protective than the native Cr-rich passive film typically formed on 304L stainless steel.
The impact of LSPwC on stainless steel corrosion resistance remains mixed across literature, largely due to variations in test conditions, LSP parameters, material grades, and evaluation techniques. For example, Peyre et al. found that LSPwC reduced the pitting resistance of 316L stainless steel in simulated saltwater, attributing the decline to severe surface roughening, selective ablation near inclusions, and residual tensile stress at the interface [50]. In contrast, Prabhakaran et al. observed that while LSPwC had minimal effect on corrosion potential and current density in 304 stainless steel, it significantly improved pitting resistance, as shown by an increased pitting potential and reduced pit severity [31]. Similarly, Kalainathan et al. reported that LSPwC led to a slight rise in corrosion current density for 316L, yet yielded a more noble corrosion potential and limited pit propagation, suggesting improved localized corrosion resistance despite a higher corrosion activity [25]. Additionally, several studies have demonstrated that LSPwC can enhance SCC resistance by introducing compressive residual stresses that suppress both crack initiation and propagation [30,32,49].
Overall, while some studies have reported improved corrosion performance following LSPwC due to the introduction of beneficial compressive residual stress, the results of the present study highlight important trade-offs associated with omitting a protective overlay. SEM–EDS analysis indicates the formation of a Fe-rich oxide layer and increased surface porosity under LSPwC conditions, which correlate with higher %DOS values and adverse shifts in ΔECORR and ΔiCORR. These observations underscore the importance of surface chemistry and morphology in governing corrosion behavior and suggest that, for applications requiring robust passivation, the use of a sacrificial coating remains advantageous.
While the present study establishes clear correlations between laser shock peening conditions and electrochemical corrosion responses, further work employing surface-sensitive techniques such as X-ray photoelectron spectroscopy (XPS) and cross-sectional scanning transmission electron microscopy (STEM) would be valuable for directly characterizing passive film chemistry and stability and to more definitively isolate the mechanisms governing passivation and repassivation behavior. In addition, LSPwC may remain a viable processing route if combined with appropriate post-processing treatments aimed at removing the oxidized layer and restoring surface integrity. As such, it may be of interest to explore the effects of varying percent overlap and other process optimizations to better understand how to control the surface response under LSPwC.
5. Conclusions
This study evaluated the effects of laser shock peening (LSP) and LSP without protective coating (LSPwC) on the microstructure and corrosion behavior of baseline and sensitized 304L stainless steel using electrochemical polarization methods. The following conclusions were drawn:
- Deformation-induced martensite was detected near the surface in both baseline and LSP-treated specimens. However, XRD analysis indicates that this transformation originated primarily from mechanical polishing rather than from the LSP process itself. The disappearance of martensitic peaks following electropolishing suggests that LSP’s high strain-rate does not heavily promote martensitic transformation in low-SFE austenitic stainless steels.
- LSP enhanced corrosion resistance in 304L stainless steel, particularly under mildly sensitized conditions (650 °C; 5 h). This improvement is attributed to compressive residual stress and increased dislocation density, which together stabilized the passive film and lowered the corrosion rate. However, under higher peening intensities and more severe sensitization (650 °C; 24 h) these benefits diminished, suggesting that further optimization of the LSP parameters is needed.
- LSPwC treatments degraded corrosion performance across all test conditions. The absence of a sacrificial overlay led to the formation of Fe-rich oxides at the surface, as confirmed by EDS and XRD, which interfered with passive film regeneration and increased corrosion susceptibility. These findings suggest that LSPwC may require additional post-processing (e.g., grit blasting or chemical cleaning) to restore surface integrity for corrosion-sensitive applications.
In summary, LSP presents a promising strategy for enhancing corrosion resistance in 304L stainless steel, especially under mild sensitization. Under the current process parameters, it offers beneficial subsurface modifications without promoting harmful martensite formation. However, its efficacy depends on process control and the material’s prior thermal and microstructural history. LSPwC, while offering processing advantages, compromises surface passivity due to laser-induced surface oxidation. Future studies should focus on optimizing LSP parameters for highly sensitized microstructures, assessing the impact of varying laser overlap and geometry, and exploring post-treatment strategies to improve the viability of LSPwC.
The novelty of this work lies in demonstrating that the corrosion response of sensitized 304L stainless steel to LSP is governed not only by residual stress and plastic deformation, but also critically by surface chemistry and processing strategy. By directly comparing LSP with and without a sacrificial coating under identical electrochemical conditions, this study highlights the trade-offs associated with simplified LSPwC processing and underscores the need to consider corrosion mode–specific responses when evaluating surface treatments for nuclear and other corrosion-sensitive applications.
Author Contributions
R.C.: Conceptualization; Methodology; Investigation; Writing—Original Draft; Visualization. V.K.V.: Conceptualization; Validation; Writing—Review and Editing; Funding Acquisition; Supervision. All authors have read and agreed to the published version of the manuscript.
Funding
This research was funded by the Nuclear Energy University Program (NEUP) of the US Department of Energy, Office of Nuclear Energy award # DE-NE0008770, administrated by the Idaho Operations office, with Dr. Kenneth Ross (PNNL) as project technical monitor.
Data Availability Statement
The original contributions presented in this study are included in the article. Further inquiries can be directed to the corresponding author.
Acknowledgments
The authors are grateful for the financial support provided by the Nuclear Energy University Program (NEUP) of the US Department of Energy, Office of Nuclear Energy award # DE-NE0008770, administrated by the Idaho Operations office, with Kenneth Ross (PNNL) as the project technical monitor. The authors acknowledge the contribution of the State of Ohio, Department of Development and Third Frontier Commission, which provided funding and support of the “Ohio Center for Laser Shock Processing for Advanced Materials and Devices”, as well as the equipment used throughout this study. The authors are also grateful to the Advanced Materials Characterization Center (AMCC) at the University of Cincinnati for the electron microscopy equipment utilized in this work for microstructural characterization.
Conflicts of Interest
The authors declare no conflicts of interest.
References
- HI-2002444; Holtec International Final Safety Analysis Report for the HI-STORM 100 Cask System. Holtec International: Marlton, NJ, USA, 2006.
- Bayssie, M.; Dunn, D.; Csontos, A.; Caseres, L.; Mintz, T. Evaluation of Austenitic Stainless Steel Dry Storage Cask Stress Corrosion Cracking Susceptibility. In Proceedings of the 14th International Conference on Environmental Degradation of Materials in Nuclear Power Systems Water Reactors, Virginia Beach, VA, USA, 23–27 August 2009; Volume 2, pp. 1452–1461. [Google Scholar]
- Caseres, L.; Mintz, T.S. Atmospheric Stress Corrosion Cracking Susceptibility of Welded and Unwelded 304, 304L and 316L Austenitic Stainless Steels Commonly Use for Dry Cask Storage Containers Exposed to Marine Engironments; Southwest Research Institute: San Antonio, TX, USA, 2010. [Google Scholar]
- Parrott, R.; Pitts, H. Chloride Stress Corrosion Cracking in Austenitic Stainless Steel: Assessing Susceptibility and Structural Integrity; Health and Safety Laboratory: Buxton, UK, 2011. [Google Scholar]
- He, X.; Mintz, T.S.; Pabalan, R.; Miller, L.; Oberson, G. Assessment of Stress Corrosion Cracking Susceptibility for Austenitic Stainless Steels Exposed to Atmospheric Chloride and Non-Chloride Salts; Southwest Research Institute: San Antonio, TX, USA, 2014. [Google Scholar]
- 3002002822; Diablo Canyon Stainless Steel Dry Storage Canister Inspection. EPRI: Palo Alto, CA, USA, 2016.
- 1025209; Calvert Cliffs Stainless Steel Dry Storage Canister Inspection. EPRI: Palo Alto, CA, USA, 2014.
- Bryan, C.; Enos, D. Results of Stainless Steel Canister Corrosion Studies and Environmental Sample Investigations; Sandia National Laboratories: Albuquerque, NM, USA, 2014. [Google Scholar]
- Enos, D.G.; Bryan, C.R. Understanding the Environment on the Surface of Spent Nuclear Fuel Interim Storage Containers; Sandia National Laboratories: Albuquerque, NM, USA, 2014. [Google Scholar]
- Gorman, J.; Fuhr, K.; Broussard, J. Literature Review of Environmental Conditions and Chloride-Induced Degradation Relevant to Stainless Steel Canisters in Dry Cask Storage Systems; EPRI: Palo Alto, CA, USA, 2014. [Google Scholar]
- Meyer, R.M.; Pardini, A.F.; Cuta, J.M.; Adkins, H.E.; Casella, A.M.; Qiao, H.; Larche, M.R.; Diaz, A.A.; Doctor, S.R. NDE to Manage Atmospheric SCC in Canisters for Dry Storage of Spent Fuel: An Assessment; Pacific Northwest National Laboratory (PNNL): Richland, WA, USA, 2013. [Google Scholar]
- Xie, Y.; Zhang, J. Chloride-Induced Stress Corrosion Cracking of Used Nuclear Fuel Welded Stainless Steel Canisters: A Review. J. Nucl. Mater. 2015, 466, 85–93. [Google Scholar] [CrossRef] [Scilit]
- Sedriks, J.A. Corrosion of Stainless Steels, 2nd ed.; Wiley: New York, NY, USA, 1996; ISBN 9780471007920. [Google Scholar]
- Frankel, G.S. Pitting Corrosion of Metals A Review of the Critical Factors. J. Electrochem. Soc. 1998, 145, 2186–2198. [Google Scholar] [CrossRef] [Scilit]
- Pascali, R.; Benvenuti, A.; Wenger, D. Carbon content and grain size effects on the sensitization of alsl type 304 stainless steels. Corrosion 1984, 40, 21–32. [Google Scholar] [CrossRef] [Scilit]
- Bain, E.C.; Abom, R.H.; Rutherford, J.J.B. The Nature and Precipitation of Intergranular Corrosion in Austenitic Stainless Steels. Trans. Am. Soc. Steel Treat. 1933, 21, 481–509. [Google Scholar]
- Enos, D.G.; Bryan, C.R. Final Report: Characterization of Canister Mockup Weld Residual Stresses; Sandia National Laboratories: Albuquerque, NM, USA, 2016. [Google Scholar]
- Larsen, E.D.; Watkins, A.D.; Mcjunkin, T.R.; Pace, D.P.; Bitsoi, R.J. Remote Welding, NDE and Repair of DOE Standardized Canisters; Idaho National Lab. (INL): Idaho Falls, ID, USA, 2006. [Google Scholar]
- Peyre, P.; Scherpereel, X.; Berthe, L.; Carboni, C.; Fabbro, R.; Béranger, G.; Lemaitre, C. Surface Modifications Induced in 316L Steel by Laser Peening and Shot-Peening. Influence on Pitting Corrosion Resistance. Mater. Sci. Eng. A 2000, 280, 294–302. [Google Scholar] [CrossRef] [Scilit]
- Peyre, P.; Braham, C.; Lédion, J.; Berthe, L.; Fabbro, R. Corrosion Reactivity of Laser-Peened Steel Surfaces. J. Mater. Eng. Perform. 2000, 9, 656–662. [Google Scholar] [CrossRef] [Scilit]
- Lu, J.Z.; Qi, H.; Luo, K.Y.; Luo, M.; Cheng, X.N. Corrosion Behaviour of AISI 304 Stainless Steel Subjected to Massive Laser Shock Peening Impacts with Different Pulse Energies. Corros. Sci. 2014, 80, 53–59. [Google Scholar] [CrossRef] [Scilit]
- Lu, J.Z.; Luo, K.Y.; Yang, D.K.; Cheng, X.N.; Hu, J.L.; Dai, F.Z.; Qi, H.; Zhang, L.; Zhong, J.S.; Wang, Q.W.; et al. Effects of Laser Peening on Stress Corrosion Cracking (SCC) of ANSI 304 Austenitic Stainless Steel. Corros. Sci. 2012, 60, 145–152. [Google Scholar] [CrossRef] [Scilit]
- Yoo, Y.-R.; Choi, S.-H.; Kim, Y.-S. Effect of Laser Shock Peening on the Stress Corrosion Cracking of 304L Stainless Steel. Metals 2023, 13, 516. [Google Scholar] [CrossRef] [Scilit]
- Guan, L.; Ye, Z.; Zhong, J.; Li, Y.; Zhang, Y. Enhancement of Corrosion Resistance of 304L Stainless Steel Treated by Massive Laser Shock Peening. Opt. Laser Technol. 2022, 154, 108319. [Google Scholar] [CrossRef] [Scilit]
- Kalainathan, S.; Sathyajith, S.; Swaroop, S. Effect of Laser Shot Peening Without Coating on the Surface Properties and Corrosion Behavior of 316L Steel. Opt. Lasers Eng. 2012, 50, 1740–1745. [Google Scholar] [CrossRef] [Scilit]
- Lu, Z.; Zhang, H.; Pan, Y.; Xu, F.; Tang, C. Effect of Laser Shock Peening on Stress Corrosion Sensitivity of 304 Stainless Steel C-Ring Weld Specimens. Mater. Res. Express 2021, 8, 016516. [Google Scholar] [CrossRef] [Scilit]
- Brandal, G.; Lawrence Yao, Y. Material Influence on Mitigation of Stress Corrosion Cracking Via Laser Shock Peening. J. Manuf. Sci. Eng. 2017, 139, 011002. [Google Scholar] [CrossRef] [Scilit]
- Wei, X.; Zhang, C.; Ling, X. Effects of Laser Shock Processing on Corrosion Resistance of AISI 304 Stainless Steel in Acid Chloride Solution. J. Alloys Compd. 2017, 723, 237–242. [Google Scholar] [CrossRef] [Scilit]
- Li, Y.; Fan, J.; Wen, J.; Nie, X.; Zhou, L. Study on the Effects of Multiple Laser Shock Peening Treatments on the Electrochemical Corrosion Performance of Welded 316L Stainless Steel Joints. Metals 2022, 12, 1215. [Google Scholar] [CrossRef] [Scilit]
- Sano, Y.; Obata, M.; Kubo, T.; Mukai, N.; Yoda, M.; Masaki, K.; Ochi, Y. Retardation of Crack Initiation and Growth in Austenitic Stainless Steels by Laser Peening Without Protective Coating. Mater. Sci. Eng. A 2006, 417, 334–340. [Google Scholar] [CrossRef] [Scilit]
- Prabhakaran, S.; Kulkarni, A.; Vasanth, G.; Kalainathan, S.; Shukla, P.; Vasudevan, V.K. Laser Shock Peening Without Coating Induced Residual Stress Distribution, Wettability Characteristics and Enhanced Pitting Corrosion Resistance of Austenitic Stainless Steel. Appl. Surf. Sci. 2018, 428, 17–30. [Google Scholar] [CrossRef] [Scilit]
- Lu, Z.; Xu, F.; Tang, C.; Cui, Y.; Xu, H.; Mao, J. Stress Corrosion Cracking Susceptibility of 304 Stainless Steel Subjected to Laser Shock Peening Without Coating. J. Mater. Eng. Perform. 2021, 30, 7163–7170. [Google Scholar] [CrossRef] [Scilit]
- Fairand, B.P.; Clauer, A.H. Laser Generation of High-Amplitude Stress Waves in Materials. J. Appl. Phys. 1979, 50, 1497–1502. [Google Scholar] [CrossRef] [Scilit]
- Fabbro, R.; Fournier, J.; Ballard, P.; Devaux, D.; Virmont, J. Physical Study of Laser-Produced Plasma in Confined Geometry. J. Appl. Phys. 1990, 68, 775–784. [Google Scholar] [CrossRef] [Scilit]
- ASTM E915-21(2021); Standard Practice for Verifying the Alignment of X-Ray Diffraction Instruments for Residual Stress Measurement. American Society for Testing and Materials: West Conshohocken, PA, USA, 2022.
- Hilley, M.E.; Larson, J.A.; Jatczak, C.F.; Ricklefs, R.E. Residual Stress Measurement by X-Ray Diffraction—SAE J784a; SAE International: New York, NY, USA, 1971; Volume 15096. [Google Scholar]
- ASTM G108-94(2015); Standard Test Method for Electrochemical Reactivation (EPR) for Detecting Sensitization of AISI Type 304 and 304L Stainless Steels. American Society for Testing and Materials: West Conshohocken, PA, USA, 2015.
- Devine, T.M. The Mechanism of Sensitization of Austenitic Stainless Steel. Corros. Sci. 1990, 30, 135–151. [Google Scholar] [CrossRef] [Scilit]
- ASTM E112-13 (2021); Standard Test Methods for Determining Average Grain Size. American Society for Testing and Materials: West Conshohocken, PA, USA, 2010.
- ASTM E975-13 (2013); Standard Practice for X-Ray Determination of Retained Austenite in Steel with Near Random Crystallographic Orientation. American Society for Testing and Materials: West Conshohocken, PA, USA, 2013.
- ASTM G102-89 (2015); Standard Practice for Calculation of Corrosion Rates and Related Information from Electrochemical Measurements. American Society for Testing and Materials: West Conshohocken, PA, USA, 2015.
- He, S.L.; Liu, Y.; Jiang, D.M. Effect of Martensite Transformation on Chemical Composition, Semiconductor Property and Corrosion Resistance of Passive Film on SAE 304 Stainless Steel. Materwiss. Werksttech. 2018, 49, 1455–1467. [Google Scholar] [CrossRef] [Scilit]
- Monrrabal, G.; Bautista, A.; Guzman, S.; Gutierrez, C.; Velasco, F. Influence of the Cold Working Induced Martensite on the Electrochemical Behavior of AISI 304 Stainless Steel Surfaces. J. Mater. Res. Technol. 2019, 8, 1335–1346. [Google Scholar] [CrossRef] [Scilit]
- Chunchun, X.; Gang, H. Effect of Deformation-induced Martensite on the Pit Propagation Behavior of 304 Stainless Steel. Anti-Corros. Methods Mater. 2004, 51, 381–388. [Google Scholar] [CrossRef] [Scilit]
- Chen, A.Y.; Ruan, H.H.; Wang, J.; Chan, H.L.; Wang, Q.; Li, Q.; Lu, J. The Influence of Strain Rate on the Microstructure Transition of 304 Stainless Steel. Acta Mater. 2011, 59, 3697–3709. [Google Scholar] [CrossRef] [Scilit]
- Langer, K.; Olson, S.; Brockman, R.; Braisted, W.; Spradlin, T.; Fitzpatrick, M.E. High Strain-Rate Material Model Validation for Laser Peening Simulation. J. Eng. 2015, 2015, 150–157. [Google Scholar] [CrossRef] [Scilit]
- Zhang, Y.; Lu, J.; Luo, K. Grain Refinement of AISI 304 SS Induced by Multiple Laser Shock Processing Impacts. In Laser Shock Processing of FCC Metals; Springer Series in Materials Science; Springer: Berlin/Heidelberg, Germany, 2013; Volume 179, pp. 153–167. ISBN 978-3-642-35673-5. [Google Scholar]
- Ralls, A.M.; Mao, B.; Menezes, P.L. Tribological Performance of Laser Shock Peened Cold Spray Additive Manufactured 316L Stainless Steel. J. Tribol. 2023, 145, 071702. [Google Scholar] [CrossRef] [Scilit]
- John, M.; Ralls, A.M.; Misra, M.; Menezes, P.L. Effect of Ultrasonic Impact Peening on Stress Corrosion Cracking Resistance of Austenitic Stainless-Steel Welds for Nuclear Canister Applications. J. Nucl. Mater. 2023, 584, 154590. [Google Scholar] [CrossRef] [Scilit]
- Peyre, P.; Carboni, C.; Forget, P.; Beranger, G.; Lemaitre, C.; Stuart, D. Influence of Thermal and Mechanical Surface Modifications Induced by Laser Shock Processing on the Initiation of Corrosion Pits in 316L Stainless Steel. J. Mater. Sci. 2007, 42, 6866–6877. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.