


Abstract
The growing demand for sustainable construction materials has intensified research on eco-efficient lightweight artificial aggregates (LWAs). This study evaluates the feasibility of producing LWAs with potential structural applicability from smectite (bentonite) clays from Paraíba, Brazil, combined with porcelain polishing residue (PPR). Raw materials were comprehensively characterized by XRD, XRF, and TGA, confirming montmorillonite as the dominant mineral phase in the clays and revealing the high silica and alumina content of the residue. The incorporation of PPR proved essential, as the clays alone could not be effectively sintered. An experimental matrix comprising ten formulations across four clay types was tested at five sintering temperatures (1100–1250 °C), resulting in 50 formulation–temperature experimental conditions. Approximately 66% of the 50 formulation–temperature experimental conditions met key physical and mechanical criteria typically associated with structural lightweight aggregates, demonstrating strong potential for use in structural lightweight concrete, although concrete-scale validation is still required to confirm their performance within cementitious mixtures. Mechanical performance was strongly influenced by thermal processing and residue incorporation, with peak strengths observed within a narrow sintering window around 1150 °C, where conditions were consistent with enhanced vitrification and pore evolution. The lightweight behavior was directly associated with the formation and expansion of internal pores during sintering, which are essential for density reduction. In this context, an optimal balance between mechanical strength and internal porosity must be achieved, since excessive densification may limit pore development. Water absorption was used as an indirect indicator of pore connectivity and internal structure evolution. An environmental assessment based on modeled production scenarios demonstrated that increasing residue content and reducing firing temperature generally reduced the calculated cumulative energy demand and global warming potential under the adopted inventory assumptions. Because thermal-energy requirements were estimated rather than directly measured in industrial kilns, the environmental results are interpreted as comparative scenario-based estimates rather than direct measurements of industrial-scale performance. Overall, the developed aggregates show strong potential for structural lightweight concrete applications, although concrete-scale validation remains necessary to confirm their performance in cementitious mixtures. This approach establishes a quantitatively grounded framework for designing low-carbon LWAs, contributing to decarbonization strategies in the ceramic and construction sectors.
1. Introduction
Urbanization and infrastructure development drive high demand for aggregates, which constitute the bulk of concrete (60–80%) [1,2]. Natural aggregate extraction stresses ecosystems, causing soil degradation [3], biodiversity loss [4], and carbon emissions from quarrying [5,6,7]. Research indicates that industrial waste, such as porcelain sludge in bricks, can enhance material properties (e.g., a 32% increase in compressive strength and improved sulfate resistance) [7,8,9,10], often attributed to phase transformations like the crystallization of mullite and pseudowollastonite [9], which improve mechanical strength [10,11], chemical durability [12], and dimensional stability of sintered materials [13].
Recent advances in hybrid material synthesis have shown that waste-derived lightweight aggregates (LWAs) can achieve a low density while maintaining sufficient mechanical strength to meet structural requirements [14]. In particular, the fine wet dust generated during the final polishing stage of porcelain tile production (Porcelain Polishing Residue, PPR) has emerged as a valuable secondary raw material [15,16]. Upon controlled firing, this residue develops a porous internal structure and a vitrified outer layer, yielding aggregates with densities below 1.80 g/cm3 and water absorption rates meeting relevant international standards, such as ASTM C330 [17]. Although these studies demonstrate the technical feasibility of waste-derived LWAs, they are predominantly focused on isolated material systems or single-performance metrics. As a result, the combined effects of raw material synergy, thermal processing, and environmental performance remain insufficiently explored in an integrated framework.
Complementary studies suggest that the presence of alkali and alkaline earth oxides in PPR acts as a fluxing agent, promoting liquid-phase sintering [18,19]. Despite these advances, a critical scientific gap persists in the literature. Existing studies rarely address the combined interaction between highly plastic smectitic clays and high-volume industrial residues under controlled thermal conditions. In particular, the role of smectite mineralogy in governing pore formation, gas entrapment, and structural stability during sintering remains poorly understood. Moreover, most prior work evaluates mechanical or environmental performance in isolation, lacking a unified framework that can simultaneously optimize both. This limitation prevents the identification of robust processing windows that reconcile lightweight performance, structural integrity, and carbon reduction.
Previous findings indicate that incorporating high levels of waste, often ranging from 50% to 90% in similar ceramic residue systems, is technically feasible for producing aggregates that fulfill the density requirements (ρd < 2.00 g/cm3) for structural applications [16,20]. The selection of the 1100–1250 °C range encompasses the critical thermal window where phase transformations, such as the formation of a low-viscosity glassy phase required to trap gases and induce bloating, typically occur in waste-clay mixtures [21]. Furthermore, while temperatures near 1100 °C often result in structural densification or shrinkage due to dehydroxylation, significant volumetric expansion is frequently reported only above 1200 °C, justifying the upper thermal limits of the current experimental matrix [16,21].
Energy efficiency is a critical parameter in the thermal processing of ceramic-based materials, particularly in high-temperature systems such as lightweight aggregate production, where firing represents the most energy-intensive stage of the lifecycle [22]. Optimizing thermal schedules not only improves process performance and cost-effectiveness but also plays a decisive role in mitigating environmental impacts, as fuel consumption during sintering is directly linked to greenhouse gas emissions and, consequently, to the material’s global warming potential [23]. In this context, recent studies highlight that partial substitution of clay with industrial residues, combined with reduced firing temperatures, can significantly reduce energy demand while maintaining adequate physicochemical performance, reinforcing the environmental and technological viability of such strategies [24,25,26,27,28].
From a sustainability perspective, defining appropriate limits for replacing clay with industrial waste, as well as optimizing sintering temperature, is essential to reconcile technical performance and environmental responsibility, ensuring that waste-derived LWAs simultaneously meet current decarbonization targets and the life-cycle assessment criteria required in sustainable materials research [26]. However, despite the recognized importance of thermal optimization, there is still a lack of studies that quantitatively couple energy demand, CO2 emissions, and mechanical performance within a statistically validated multi-response optimization framework. This gap limits the ability to define scientifically robust processing conditions and assess their potential environmental implications under clearly stated scaling assumptions.
Paraíba State, in northeastern Brazil, is the leading producer of bentonite, responsible for approximately 87% of the country’s output [27]. This regional abundance, coupled with the proximity of industries that generate PPR, presents a unique opportunity to integrate sustainable resources. Therefore, this study aims to investigate the combined effects of smectite clay mineralogy, porcelain polishing residue (PPR) content, and sintering temperature on the physical, mechanical, and environmental performance of lightweight artificial aggregates, with particular emphasis on their potential for structural lightweight concrete applications. The specific objectives are to: (i) characterize four smectite clays and determine their suitability for lightweight aggregate production when combined with PPR; (ii) quantify the effects of PPR content and sintering temperature on expansion, density, water absorption, porosity, and mechanical strength; (iii) identify the processing variables that most strongly govern aggregate performance using statistical analysis; and (iv) determine an optimized processing condition that balances mechanical performance and environmental impact through multi-response desirability optimization.
The study is guided by three main hypotheses. First, the incorporation of PPR is expected to promote vitrification and pore development during sintering, enabling smectite-based formulations to achieve the combination of low density and mechanical strength required for lightweight aggregate applications; second, PPR content and sintering temperature are expected to exert significant effects on aggregate properties, with an optimum processing window arising from the balance between pore formation and matrix densification; and third, the integration of high PPR incorporation with optimized thermal processing is expected to reduce energy demand and CO2 emissions while maintaining adequate mechanical performance. Testing these hypotheses through an integrated experimental, statistical, and environmental framework provides a basis for defining scientifically supported processing conditions for waste-derived lightweight aggregates.
To test these hypotheses, expansion, water absorption, density, and mechanical strength were selected as key indicators of aggregate performance, as they collectively describe the development and stability of the internal pore structure and its relationship with mechanical behavior. In parallel, energy demand and global warming potential were evaluated to quantify the environmental consequences of the processing conditions. ANOVA was used to identify the relative influence of clay type, PPR content, and sintering temperature, while multi-response desirability optimization was applied to identify processing conditions capable of simultaneously improving mechanical performance and reducing environmental impact.
2. Materials and Methods
2.1. Materials
This study examined the combination of porcelain polishing residue (PPR) with four smectitic clays: Bentogel (BTG), Calcium Bentonite (BTCL), Sodium Bentonite (BTSD), and Bofe (BF). BTG, BTCL, and BTSD were commercially obtained from BENTONISA—Bentonita do Nordeste S/A (Boa Vista, Paraíba, Brazil). BTCL and BTSD were used as received, without additional chemical activation or modification by the authors. BF clay was collected in its natural state from a deposit in Cubati, Paraíba. PPR was collected directly from a porcelain tile factory in João Pessoa, Paraíba, Brazil.
BTCL and BTSD were identified according to their commercial designations as calcium bentonite and sodium bentonite, respectively. However, the exchangeable-cation composition and cation-exchange capacity of the clays were not independently determined in the present study. Therefore, the possible influence of interlayer cation chemistry on thermal expansion and pore development is recognized but was not quantitatively isolated from the effects of clay mineralogy, chemical composition, particle size, PPR content, and sintering temperature.
The selection of the clays used in this study was based on their distinct mineralogical compositions, particularly the predominance of smectitic phases, which are known to exhibit high plasticity and significant gas retention capacity during thermal treatment. This behavior is critical for promoting pore formation in lightweight aggregates. Unlike more commonly studied kaolinitic clays, smectitic clays remain underexplored in the production of lightweight aggregates, especially when combined with high volumes of industrial residues [6,16,25]. Therefore, their selection enables the investigation of alternative expansion mechanisms and helps address existing gaps in the literature.
Compared with kaolinitic clays, which typically exhibit lower plasticity and limited gas retention during sintering, smectitic clays offer greater expansion potential due to their layered structure and higher interlayer water content. Illitic clays, although more stable thermally, generally do not promote sufficient bloating without additives [6]. Therefore, the selected clays represent a deliberate choice to investigate a less explored but potentially more efficient route for pore generation in lightweight aggregates.
2.2. Methods
An experimental matrix was prepared to evaluate four clay types (BTG, BTCL, BTSD, and BF). Table 1 details the experimental design, including clay type, mix proportions, and sample coding. All compositions were sintered at five temperatures (1100, 1150, 1200, 1225, and 1250 °C). Samples are labeled using a coding system where the first number indicates PPR content (wt.%) and the second indicates sintering temperature (°C); for example, 60_1100 represents a composition with 60 wt.% PPR and 40 wt.% clay, sintered at 1100 °C.
Table 1.
Condensed experimental design and sample coding.
2.2.1. Aggregate Formulation and Preparation
The dry components were carefully mixed according to the formulation specifications. Water was then added at approximately 32 wt.% of the dry mixture mass, using the same water-to-dry-solid ratio for all clay–PPR formulations to ensure consistent granule preparation. The water was incorporated gradually during mixing until homogeneous plasticity and consistency suitable for shaping were achieved. This standardized water content was maintained across the different clay–PPR mixtures to minimize variations in initial moisture conditions that could affect pellet formation, drying behavior, pore development, and the resulting physical and mechanical properties of the LWAs. Samples were then stored in bags for 24 h to allow moisture equilibration and homogenization. After resting, approximately 6 g of pellets were manually shaped and slowly air-dried at room temperature for 5 days, followed by a final 24-h oven-drying at 105 °C. Pellets were weighed and measured immediately after oven drying, before sintering.
2.2.2. Sintering Process
Sintering was performed at five maximum temperatures, with samples heated at 10 °C/min and held for 15 min at each peak temperature [6]. Pellets were furnace-cooled to prevent cracking or deformation. Initial and final measurements were used to calculate the swelling index and loss on ignition.
Although industrial lightweight aggregate production typically involves longer residence times in rotary kilns, the present study used a 15-min holding time as an experimentally defined laboratory processing condition. This condition was selected to investigate the effects of the sintering temperature under controlled laboratory conditions and was not assumed to reproduce the residence-time, heat-transfer, or thermal-efficiency characteristics of an industrial rotary kiln [6]. Moreover, previous studies have demonstrated that pore formation and vitrification in clay–residue systems occur within narrow temperature-time windows, making short dwell times sufficient to capture the governing mechanisms of expansion and densification. Therefore, the selected holding time ensures experimental feasibility while maintaining representativeness of the critical sintering phenomena.
2.2.3. Raw Material and Lightweight Aggregate (LWA) Characterization
Starting raw materials were characterized through physical, chemical, mineralogical, and thermal analyses, and the resulting lightweight aggregates (LWAs) were evaluated for their physical and mechanical properties. All tests were conducted in accordance with the relevant national (NBR) and international (ASTM/ISO/ACI) standards to ensure data reliability and comparability (Table 2).
Table 2.
Tests were conducted on the materials used and on the LWAs produced in this study.
The chemical and physical properties of the four clays and PPR were determined using standard laboratory methods. Particle size distribution was measured using laser granulometry (CILAS 1090, 0.1–500 μm, CILAS, Orléans, France). Plasticity limits were determined according to Brazilian standards NBR 7180 [29] and NBR 6459 [30] for plastic limit and liquid limit, respectively. Mineralogical composition was analyzed by X-ray diffraction (XRD 7000, Shimadzu, Tokyo, Japan) using CuKα radiation (λ = 1.5418 Å) at 30 kV and 30 mA, from 5° to 55° 2θ (1°/min, 0.02 2θ step). The chemical composition of raw materials (≤N°. 200 mesh) was analyzed by X-ray fluorescence (BRUKER S2 PUMA—SERIES II spectrometer, Bruker, Tokyo, Japan). Thermal analysis (TG/DTA) was performed to evaluate mass loss during dehydration, dehydroxylation, and other thermal events under a nitrogen atmosphere (100 mL/min) at 10 °C/min from 25 to approximately 1100 °C, using alumina cells and approximately 10 mg samples. Microstructural and microtopographical analyses of the fractured surfaces of the sintered LWAs were performed using a TESCAN VEGA fourth-generation LMS scanning electron microscope (SEM), (Tescan Vega, Brno, Czech Republic). Images were acquired in wide-field scanning mode at 20 kV and magnifications from 37× to 3000× to investigate pore morphology, vitrification degree, and the integration of PPR into the clay matrix.
Lightweight aggregate characterization included evaluation of expansion, mass loss, density, deformation modulus, crush resistance, water absorption, apparent open porosity, and unit weight. Each test was performed on 30 individual aggregates, and results are reported as the mean ± standard deviation. The observed variability reflects the inherent heterogeneity associated with pore formation during sintering. Water absorption and apparent open porosity were used as complementary indicators of the accessible pore structure and were subsequently related to mechanical performance through correlation analysis.
2.2.4. Experimental Matrix Flowchart
Table 3 summarizes the experimental framework for evaluating the synergy between regional clays and industrial waste.
Table 3.
Experimental characterization matrix.
To optimize lightweight aggregate (LWA) properties, four Paraíba clays (BTG, BTCL, BTSD, and BF) were blended with porcelain polishing residue (PPR) using 10 formulations in total, as detailed in Table 1. BTG and BTSD were evaluated at 60% and 90% PPR, whereas BTCL and BF were evaluated at 30%, 60%, and 90% PPR. Each formulation was sintered at five peak temperatures (1100, 1150, 1200, 1225, and 1250 °C), resulting in 50 formulation–temperature experimental conditions. The mixtures were manually pelletized into approximately 6 g samples, dried in two stages (5 days at room temperature, followed by 24 h at 105 °C), and sintered at a heating rate of 10 °C/min. Each experimental condition was evaluated using 30 individual pellets, resulting in a total of 1500 specimens (50 conditions × 30 pellets per condition). The 50 experimental conditions constituted the final dataset used for the subsequent physical, mechanical, and statistical analyses. The clays provide the aluminosilicate matrix and montmorillonite for expansion but require PPR as a fluxing agent (5.85% MgO and 2.06% K2O) to lower the melting point. This induces a low-viscosity glassy phase that traps gases, leading to “bloating” and yielding a lightweight, high-strength structural material [35,36,37,38].
2.2.5. Environmental Performance
The environmental assessment was conducted as a scenario-based cradle-to-gate Life Cycle Assessment (LCA) normalized to 1 tonne of final sintered lightweight aggregate. The assessment was not based on direct measurements from an operating industrial kiln. Instead, the experimentally determined formulations, moisture conditions, mass losses, and sintering temperatures were used to define the modeled production scenarios, while the associated energy requirements were calculated using the adopted mass balances and specific thermal-energy assumptions.
The laboratory experiments therefore served as the basis for defining the material formulation and thermal-processing conditions, whereas the environmental inventory was normalized to the defined 1-tonne reference flow. The conversion from the experimental scale to this reference flow was performed using the measured formulation proportions and the adopted 10% process-loss assumption. This mathematical scaling changes the quantity of material represented in the inventory but does not imply that laboratory and industrial kilns have equivalent thermal efficiencies, heat-transfer characteristics, residence times, loading conditions, or heat-recovery efficiencies.
The reference flow was defined as 1 tonne of final sintered lightweight aggregate. This mass basis was used to normalize material inputs, energy demand, transportation, and environmental impacts across all modeled scenarios. The results should therefore be interpreted as scenario-based estimates under the defined assumptions rather than as direct measurements or validated predictions of industrial-scale production performance.
The Life Cycle Assessment (LCA) was conducted in accordance with ISO 14040 [39] and ISO 14044 [40], adopting an attributional, process-based approach. Primary experimental data were combined with secondary data obtained from the Brazilian Construction Environmental Performance Information System (SIDAC) [41]. The assessment considered global warming potential (GWP) and cumulative energy demand as the principal environmental indicators.
The same reference flow, system boundaries, and calculation procedure were applied to all clay–PPR formulations and to the commercial expanded-clay reference. This common basis was adopted to ensure consistency in the comparative assessment. However, the comparison represents a comparison between modeled production scenarios and should not be interpreted as direct evidence that the developed aggregates would exhibit lower energy consumption or GWP under actual industrial kiln operation.
All life cycle calculations were performed using a spreadsheet-based approach (Microsoft Excel), in which process activity data were directly multiplied by emission and energy factors. No dedicated LCA software (e.g., SimaPro, GaBi, or OpenLCA) was employed. This approach ensures full transparency and traceability of the calculations, while providing a cost-effective, reproducible methodology without compromising the reliability of the results [42,43,44].
The Life Cycle Assessment (LCA) calculations were performed using a spreadsheet-based approach (Microsoft Excel). Secondary data for emission and energy factors were obtained from the Brazilian Construction Environmental Performance Information System (SIDAC), ensuring regional representativeness. Each combination of clay type, PPR substitution level, and firing temperature was treated as an independent scenario. Life Cycle Impact Assessment (LCIA) was performed using the IPCC 2013 method (100-year horizon) [45], with results expressed in kg CO2-eq per functional unit. In addition to GWP, energy efficiency indicators were applied.
The study aimed to evaluate and compare the environmental impacts associated with LWAs produced from four natural clays (BTG, BTCL, BTSD, and BF), partially replaced with PPR (30–90%) and sintered at 1100–1250 °C, in comparison with Brazilian commercial expanded clay (CC) [42,43,44]. The commercial expanded-clay reference (CC) was produced in Várzea Paulista/SP using a 100% clay mixture. The sintering process was conducted at 1250 °C for 15 min, with a water content of 40%. The information is reported in reference [44]. Transportation was modeled as road transport using a two-axle truck over a 20 km distance, based on typical regional supply chain conditions. This assumption represents a simplified and conservative scenario for comparative purposes.
The functional unit was defined as 1 tonne of sintered ceramic material meeting the minimum physico-mechanical requirements experimentally verified for structural lightweight concrete. A 10% process loss between input and output mass was considered for inventory quantification. System boundaries followed a cradle-to-gate approach, including raw material extraction and processing, transportation, mixing, shaping, drying, and firing, as well as electricity and thermal energy consumption (Table 4). The use phase, end-of-life stage, infrastructure, and maintenance were excluded due to their marginal contribution and lack of influence on the comparative assessment.
Table 4.
Modeled life-cycle inventory (LCI) input data for the cradle-to-gate production scenarios normalized to 1 tonne of sintered LWA.
The energy consumption values presented in Table 4 represent modeled process-energy requirements normalized to 1 tonne of final lightweight aggregate. The calculation incorporates the material mass balance, moisture removal during drying, the investigated sintering temperatures, and the adopted specific thermal-energy requirements. The scaling procedure therefore changes the reference quantity from the laboratory batch to the defined 1-tonne reference flow but does not assume that laboratory and industrial kilns have identical thermal efficiencies, heat-transfer characteristics, residence times, loading conditions, or heat-recovery efficiencies.
Accordingly, the values reported in Table 4 should be interpreted as scenario-based estimates rather than direct measurements of industrial kiln energy consumption. The same assumptions, reference flow, and system boundaries were applied to all formulations and to the commercial expanded-clay reference to maintain internal consistency in the comparative assessment.
The results are therefore intended for comparative analysis within the defined system boundaries and assumptions and should not be interpreted as direct measurements or validated predictions of industrial kiln performance.
It can be observed in Table 4 that, from drying to sintering (1250 °C), no energy factor is reported. This is because these stages are already expressed directly in MJ, representing the final thermal energy consumed. Therefore, no additional conversion factor is required, unlike electricity (kWh) or transport (t·km). Overall, the thermal stages tend to dominate both the GWP and the total energy demand, particularly as the sintering temperature increases, reflecting the higher specific consumption of natural gas. The electricity profile corresponds to the Brazilian national grid, as defined in SIDAC, incorporating the country’s energy mix (predominantly hydroelectric with complementary fossil sources).
The thermal energy consumption values adopted for drying and sintering are based on laboratory-scale conditions, reflecting the experimental processing used in this study. These values were modeled as specific energy demand (MJ/kg) as a function of temperature and supported by the literature and database references. Therefore, they do not represent direct measurements from industrial kilns. The results are intended for comparative analysis within the defined system boundaries, and no direct extrapolation to industrial-scale production is assumed.
This integrated framework enabled the identification of ceramic formulations with improved balance between environmental impact, energy efficiency, and technical performance, supporting decision-making for low-carbon ceramic materials. Finally, the results were quantitatively analyzed, and statistical analysis was performed to assess their reliability.
Thermal-Energy Sensitivity Analysis
Because drying and sintering represent the dominant thermal-energy inputs in the modeled inventory, a sensitivity analysis was performed to evaluate the influence of the adopted thermal-energy assumptions on the calculated environmental results. The base-case thermal-energy requirements for drying and sintering were systematically varied by −20% and +20%, generating three scenarios: lower energy demand (−20%), base case, and higher energy demand (+20%).
The sensitivity analysis was applied consistently to the thermal-energy inputs of the clay–PPR formulations and to the corresponding comparative scenarios. Electricity, transportation, raw-material inputs, emission factors, and system boundaries were kept unchanged. The cumulative energy demand and GWP were recalculated for each thermal-energy scenario.
The ±20% variation was adopted as a scenario-based sensitivity range to assess the robustness of the comparative conclusions to changes in the assumed thermal-energy demand. This range does not represent a statistically estimated measurement uncertainty because direct industrial kiln energy-consumption data were not available. Instead, it provides a transparent assessment of the dependence of the environmental results on the adopted thermal-energy assumptions.
2.2.6. Statistical Analysis
A multifactor ANOVA (α = 0.05) was conducted to evaluate the statistical significance and relative contribution of the main effects of clay type, PPR content, and sintering temperature on CO2 emissions and mechanical strength. F-values, p-values, and percentage contributions to the total variance were determined for the main effects included in the model.
To complement the ANOVA, main-effects plots were generated to illustrate the influence of each factor level on CO2 emissions and mechanical strength, averaging the remaining variables. Interaction plots were also constructed (clay type × temperature, temperature × residue content, and clay type × residue content) as graphical exploratory analyses of the combined effects of the factors. These plots were used to visualize response patterns and potential synergistic or antagonistic trends, but interaction effects were not subjected to formal statistical significance testing.
Because mechanical performance and environmental impact represent competing responses, a multi-response optimization based on the desirability function was performed to simultaneously maximize crush resistance and minimize total CO2 emissions. For each response, an individual desirability function was used to transform the predicted response into a dimensionless scale ranging from 0 to 1, where 0 represents the least desirable outcome and 1 represents the most desirable outcome within the defined optimization range.
Crush resistance was defined as a maximization response, whereas total CO2 emissions were defined as a minimization response. Both responses were assigned equal importance (weight = 1) to prevent preferential weighting of either mechanical or environmental performance. The overall desirability was calculated as the weighted geometric mean of the individual desirabilities:
where D is the composite desirability, d1 is the desirability of crush resistance, and d2 is the desirability of total CO2 emissions. Under equal weighting, the geometric-mean formulation requires both responses to contribute positively to the composite desirability; consequently, a highly favorable value for one response cannot fully compensate for an unfavorable value of the other.
D = (d1 × d2)1/2
The present approach is a desirability-based multi-response optimization rather than a classical multi-criteria decision analysis (MCDA). The two responses were transformed into individual desirability values and combined into a single composite desirability index using a weighted geometric mean. Thus, the two-response problem was reduced to a single scalar objective for identifying the optimal condition within the investigated experimental domain. Classical MCDA methods, such as AHP, TOPSIS, ELECTRE, and PROMETHEE, as well as Pareto-based optimization, were not applied in the present study.
The optimization was conducted within the experimentally investigated ranges of clay type, PPR content, and sintering temperature. The condition providing the highest composite desirability was selected as the optimum. The predicted optimum was subsequently compared with the corresponding experimental result to assess the consistency of the optimization model. Accordingly, the reported optimum represents a domain-restricted solution under the adopted equal-weight desirability criterion rather than an absolute optimum independent of the selected weighting scheme.
To assess the robustness of the selected optimum to the weighting scheme, a sensitivity analysis was performed by varying the relative weights assigned to crush resistance and total CO2 emissions. Three weighting scenarios were evaluated: 0.25/0.75, 0.50/0.50, and 0.75/0.25 for mechanical/environmental performance, respectively. For each scenario, the composite desirability was recalculated using the weighted geometric mean, and the resulting optimal process conditions were compared. This analysis was used to determine whether the selected optimum was stable or substantially dependent on the relative importance assigned to the two competing objectives.
Correlation analysis was additionally performed to evaluate the relationships among apparent open porosity, water absorption, and crush resistance. Pearson’s correlation coefficient (r) was used to quantify the linear association between the variables, with statistical significance evaluated at α = 0.05. The correlations were calculated using the mean values of the 50 experimental conditions for which porosity, water absorption, and crush resistance were available.
3. Results and Discussion
3.1. Characterization of Materials
Figure 1 shows the particle-size distribution of the raw materials. Bofe clay (BF) had the largest particle size, while porcelain polishing residue (PPR) exhibited a fine distribution, consistent with prior research [45,46,47,48]. This fine PPR particle size is crucial for sintering, enhancing particle packing, increasing contact area, and promoting early viscous flow [49]. The other clays (BTG, BTCL, and BTSD) had particle sizes considerably larger than those of the PPR. This size difference is beneficial for lightweight aggregate (LWA) production, as replacing coarser clay particles with finer PPR improves packing density [50]. This improved packing promotes pyroplastic deformation during sintering, while coarser particles aid gas retention for pore formation and expansion [51,52].
Figure 1.
Particle size distribution of the clays and PPR used.
The materials, primarily composed of SiO2 (64.46–70.45%) and Al2O3 (19.32–25.19%) (Table 5), form a refractory aluminosilicate framework crucial for aggregate applications. Notably, PPR exhibits the highest Al2O3 content (25.19%). Minor oxides, including Fe2O3, MgO, CaO, K2O, and Na2O, function as fluxing agents, effectively lowering the melting temperature of the SiO2/Al2O3 blend [16,53]. The elevated MgO (5.85%) and K2O (2.06%) concentrations in PPR likely facilitate the formation of a low-viscosity glassy phase, which is necessary for sintering, a process not achievable with raw clays alone. Fusion index (k) values, ranging from 5.84 (BTCL) to 10.17 (BF), demonstrate an inverse correlation with melting points [54]. Therefore, BTCL and BTSD (k = 5.84 and 6.45, respectively) are expected to exhibit superior performance at lower temperatures than BF (k = 10.17), a conclusion supported by LWA testing.
Table 5.
Chemical analysis of the samples.
XRD analysis (Figure 2) identified montmorillonite as the primary clay mineral in all samples. Montmorillonite, common in bentonite clays, has a high interlayer water content. Its rapid release of water and hydroxyl groups during heating, combined with a viscous glassy phase from the PPR [16], induces the expansion necessary for LWA production. The PPR’s quartz enhances the composite’s dimensional stability, while SiC is derived from polishing abrasives. Crucially, mullite, which forms needle-like structures during high-temperature crystallization, acts as a structural skeleton, contributing to the high mechanical strength of the final LWA products [54,55,56].
Figure 2.
XRD results of the samples.
TGA-DTA results (Figure 3) showed that major mass losses for all raw materials occurred below 900 °C, with total mass losses varying significantly: 18–18.5% for BF and BTG, 17% for BTCL, 13.5% for BTSD, and only 2.5% for PPR. The higher losses in clayey materials are attributed to the release of adsorbed water and dehydroxylation of clay minerals [16]. Conversely, PPR’s minimal mass loss reflects its crystalline composition, mainly quartz, mullite, and silicon carbide (Figure 2). These thermally stable phases do not undergo dehydration or dehydroxylation, leading to little mass change [57]. The absence of clay minerals in PPR explains its featureless DTA curve and high thermal stability [58].
Figure 3.
Simultaneous thermal analysis (TG/DTA): (a) BTG; (b) BTCL; (c) BTSD; (d) BF; (e) PPR.
3.2. Performance of Lightweight Artificial Aggregates (LWAs)
In this framework, expansion index and water absorption were adopted as primary indicators of lightweight performance, since they capture the balance between pore generation and densification. At the same time, vitrification was inferred to play a role in the development of lightweight aggregates with improved performance. Conversely, excessive pore expansion may weaken the structure. Therefore, the expansion index and water absorption were adopted as primary indicators, since they reflect conditions under which internal pores are generated and stabilized without structural collapse.
The physical and mechanical properties of the LWAs are discussed below, with emphasis on the relationships among PPR content, sintering temperature, and aggregate performance. Structural LWAs typically require an apparent specific mass (ASM) ≤ 2.00 g/cm3 and a tensile or crushing resistance ≥ 2.30 MPa [17,59].
To quantitatively evaluate the role of porosity in the physical and mechanical performance of the lightweight aggregates, correlation analyses were performed using the mean values of the 50 experimental conditions for which apparent open porosity, water absorption, and crush resistance were available. Apparent open porosity showed a statistically significant positive correlation with water absorption (r = 0.443, p = 0.001), indicating that greater accessible pore volume was generally associated with greater water uptake. Apparent open porosity also showed a statistically significant negative correlation with crush resistance (r = −0.345, p = 0.014). However, the relatively low coefficient of determination (R2 = 0.119) indicates that porosity alone explains only a limited fraction of the variation in mechanical resistance. In contrast, water absorption was not significantly correlated with crush resistance (r = 0.075, p = 0.603).
These results indicate that the amount of porosity is an important but not exclusive descriptor of aggregate performance. Water absorption depends on the accessibility and connectivity of the pore network, whereas mechanical resistance is additionally influenced by pore size, shape, distribution, connectivity, and the degree of matrix vitrification. Consequently, aggregates with comparable porosity may exhibit different mechanical responses when their pore architectures differ. The correlation results therefore complement the SEM observations and quantitative image analysis presented below.
BTG performs optimally at approximately 1150 °C (Figure 4). The reduction in water absorption and apparent density suggests the occurrence of vitrification-related processes. However, pore sealing and internal gas entrapment are inferred from indirect evidence and cannot be conclusively confirmed without detailed microstructural or phase analysis. This condition, therefore, should not be interpreted as maximum densification, but rather as a transitional stage where sufficient vitrification enables gas entrapment while still allowing controlled pore expansion. Thus, the optimal condition at 1150 °C reflects a balance between densification and the development of internal porosity, rather than densification alone [60]. This behavior indicates the initial stage of pore sealing and densification, before significant internal expansion. At slightly higher temperatures, the generation and stabilization of internal pores become dominant, promoting the reduction in density required for lightweight performance.
Figure 4.
Properties for BTG clay LWAs. Note: † Extreme observed value; not representative of the typical crush resistance of the BTG–90% PPR formulation at 1150 °C.
The BTG 90% PPR formulation exhibited an extreme observed crush resistance of 27.68 MPa† at 1150 °C. However, the coexistence of this high strength with a very low density (~1.0–1.2 g/cm3) is unusual and therefore requires cautious interpretation. Each formulation–temperature condition was evaluated using 30 individual aggregates, reducing the likelihood that the reported value resulted solely from a single anomalous specimen. Nevertheless, the relatively high residual contribution in the ANOVA (40.36%) indicates substantial experimental variability that is not explained by the investigated factors. Such variability may arise from stochastic pore formation and differences in local pore architecture during sintering.
In particular, an individual aggregate may exhibit a favorable combination of a mechanically strong vitrified matrix or outer region and closed internal pores, resulting in an unusually high strength-to-density ratio. At the same time, the present data do not allow a measurement artifact or non-representative microstructural region to be completely excluded. Therefore, the 27.68 MPa† value should be regarded as an extreme observed value rather than as a typical or representative strength for BTG aggregates at this density. Confirmation of its representativeness would require independent-batch replication and specimen-level correlation between density, pore morphology, and crush resistance.
In summary, LWA performance is controlled by a critical thermochemical window defined by PPR content and sintering temperature. Between 1150 and 1200 °C, the observed behavior is consistent with vitrification-assisted pore evolution. However, the underlying mechanisms are inferred from indirect observations, with the observed behavior characterized by sharply reduced water absorption and specific mass and maximized strength. Below this range, densification is incomplete; above it, excessive expansion increases porosity and weakens the structure. Higher PPR contents enhance lightness but require this optimal thermal range to maintain mechanical performance. Overall, 90% PPR at 1150 °C represents the best balance of properties, indicating that precise sintering control is critical for achieving a balance between density reduction and mechanical performance. This confirms that optimal lightweight performance is not achieved by maximum densification, but by a balance between internal pore generation and mechanical stability.
BTCL exhibits high sensitivity to increases in temperature, as shown by its low fusion index (k = 5.84, Table 5, Figure 5). Effective pore sealing results in a rapid decrease in water absorption and apparent porosity between 1100 and 1150 °C [7]. Specifically, for BTCL 90% PPR, absorption decreases sharply from 11.65 to 0.04%, suggesting a fluxing effect of PPR within the clay matrix at 1150 °C [14].
Figure 5.
Properties for BTCL clay LWAs.
The maximum tensile resistance for both 60 and 90% PPR is observed at 1150 °C (26.34 and 23.46 MPa, respectively), indicating that this temperature yields the maximum observed mechanical strength under the tested conditions before bloating weakens the ceramic matrix. This highlights a narrow processing window for optimal mechanical performance [61,62].
The results confirm that aggregate performance is strongly governed by the combined effects of composition and sintering temperature, with a well-defined thermal optimization range. Around 1150 °C, the materials exhibit the best balance between expansion and densification, expressed by moderate bloating, low water absorption, reduced density, and peak mechanical strength. At lower temperatures, insufficient sintering limits structural cohesion, whereas higher temperatures promote excessive expansion, increasing porosity and mass loss and consequently reducing strength and stiffness. Variations among mixtures indicate that compositional adjustments modulate gas generation and viscous flow. Still, optimal performance is achieved only within this narrow processing window, reinforcing the idea that precise thermal control is the key parameter for producing high-performance lightweight aggregates.
The commercially supplied sodium bentonite (BTSD) exhibited high mechanical strength at intermediate temperatures (Figure 6). As observed for BTCL, the reduction in apparent porosity and water absorption between 1100 and 1150 °C suggests the development of a more consolidated and less permeable structure during sintering. The specific contribution of the interlayer cation composition to this behavior, however, cannot be isolated because exchangeable-cation composition and cation-exchange capacity were not experimentally determined in the present study.
Figure 6.
Properties for BTSD clay LWAs.
The peak crush resistance of BTSD 90% PPR (27.95 MPa) coincides with the maximum shrinkage and density at 1150 °C, indicating a favorable sintering condition within the tested range. Above this temperature, strength decreases and expansion increases, suggesting bloating and structural relaxation due to increased porosity [61,62,63]. The reduced sintering temperature lowers energy consumption and production costs [47,48,64], offering a technological and socioeconomic advantage, particularly in Northeastern Brazil (João Pessoa/PB), where traditional ceramic production relies on energy-intensive firing. Furthermore, increased incorporation of PPR waste reduces costs and enhances waste valorization, as confirmed by life-cycle assessment results, thereby demonstrating the material’s environmental and economic feasibility.
BF clay, characterized by its coarse particle size and high fusion index (k = 10.17), necessitated higher temperatures or increased residue for successful application (Figure 7). The formulation containing 30% PPR failed to meet the water-absorption limit at 1100 °C (26.5%). The steadily increasing ASM up to 1250 °C, coupled with minimal swelling and consistent shrinkage, suggests under-fluxing [31].
Figure 7.
Properties for BF clay LWAs.
Coarse particles and a high k value hinder the formation of the glassy phase, preventing gas entrapment and expansion, even at high temperatures [37]. The PPR acts as a sintering aid, as demonstrated by BF 90% PPR achieving peak strength earlier at 1150 °C (17.79 MPa). This shows that increased PPR accelerates the reaction kinetics and lowers the optimal vitrification temperature, effectively counteracting the clay’s refractoriness [16,64]. Consequently, BF clay generally requires higher processing temperatures than bentonites to meet LWA requirements, confirming the impact of raw material chemistry and particle size on the final product.
Clay mineralogy, PPR content, and sintering temperature significantly influence lightweight aggregate performance, as shown in Figure 4, Figure 5, Figure 6 and Figure 7. Bentonite clays (BTG, BTCL, and BTSD), high in montmorillonite, exhibited optimal performance around 1150 °C due to effective pore sealing, controlled expansion, and high mechanical strength. BTCL and BTSD were more sensitive to temperature changes, consistent with their lower fusion indices and higher PPR fluxing efficiency. Conversely, BF clay, with its coarser particles and higher fusion index, required higher temperatures or more PPR to achieve similar vitrification and strength, indicating its more refractory nature.
PPR content significantly influences sintering in clay systems. Low PPR hinders vitrification at lower temperatures, causing high water absorption and minimal bloating, especially in BF clay. Higher PPR promotes a low-viscosity glassy phase, improving pore entrapment and expansion, and lowering the optimal sintering temperature. However, excessive PPR at high temperatures results in over-firing, excessive bloating, and reduced mechanical strength. Therefore, balancing clay type, PPR content, and firing temperature is crucial for producing structural lightweight aggregates; BTSD clay with 90% PPR sintered at 1150 °C offers the best balance of performance, energy efficiency, and waste valorization.
Microstructural analysis via SEM (Figure 8) provided additional evidence supporting the relationship between internal pore morphology and the macroscale properties of the LWAs. These observations confirm that lightweight behavior is primarily governed by the formation and stabilization of internal pores rather than by maximum densification alone, supporting a controlled bloating mechanism This transition from densification to bloating is clearly driven by the degree of vitrification and pore evolution. These observations confirm that lightweight behavior is primarily governed by the formation and stabilization of internal pores, rather than by maximum densification, supporting the interpretation of a controlled bloating mechanism. The transition from densification to bloating is clearly governed by the degree of vitrification and pore evolution. In the BTG 60% PPR (1200 °C) samples (Figure 8a,b), a high concentration of spheroidal pores was observed.
Figure 8.
SEM BTG at 1200 °C (a,b), BTCL at 1100 °C (c,d), BTSD at 1200 °C (e,f), and BF at 1200 °C (g,h) samples with 60% PPR.
The smooth, rounded edges of these pores are consistent with a vitrification-related process, where the liquid phase’s surface tension facilitates pore spheroidization. The predominantly spherical and apparently non-interconnected pore morphology may contribute to the relatively high mechanical resistance observed under favorable processing conditions, since rounded pores are generally expected to produce less severe stress concentrations than irregular or sharply connected cavities. This highly spherical and isolated pores observed in the analyzed BTG samples are consistent with the possibility of closed porosity contributing to the combination of low density and mechanical integrity. However, because the SEM observations were obtained for the BTG 60% PPR formulation at 1200 °C, they should not be considered direct microstructural validation of the 27.68 MPa value measured for BTG 90% PPR at 1150 °C. Therefore, the relationship between pore morphology and the exceptionally high strength-to-density ratio remains a plausible interpretation rather than a demonstrated causal mechanism.
The BTCL 60% PPR (1100 °C) samples exhibited a network of interconnected, irregular cavities and sharp-edged protrusions (Figure 8c,d). This topography indicates incomplete vitrification at lower temperatures, where the liquid phase was insufficient to seal the pores. This microstructural state directly correlates with the higher water absorption rates recorded at 1100 °C, as the lack of a continuous glassy “skin” allows for fluid penetration.
The SEM images of the BTSD samples reveal a sponge-like internal structure with a uniform distribution of pores (Figure 8e,f). While some unreacted angular PPR particles remain visible—indicating that the residue acts partially as a refractory filler—the formation of oval and spherical pores at 1150–1200 °C explains the ideal balance of low bulk density (1.91 g/cm3) and high crush resistance (16.78 MPa). The presence of these pores supports the hypothesis of pyroplastic deformation triggered by the PPR’s fluxing oxides (MgO and K2O).
In contrast, the BF 60% PPR (1200 °C) aggregates showed significant structural heterogeneity, with interconnected ellipsoidal pores and extensive microfractures traversing the matrix (Figure 8g,h). This microtopography suggests that the high fusion index (k = 10.17) of the Bofe clay hindered uniform vitrification, creating zones of fragility that explain its lower resistance compared to the bentonite-based aggregates.
Quantitative image analysis of the SEM micrographs was performed using ImageJ software, version 1.54g. The resulting parameters are summarized in Table 6 and provide quantitative support for the morphological differences observed among the formulations. The high-magnification images (Figure 8b,d,f,h) were calibrated according to their respective scale bars and converted to 8-bit grayscale.
Table 6.
Quantitative pore morphology parameters obtained from SEM images using ImageJ. Apparent open- and closed-pore fractions refer to the projected pore area classified according to two-dimensional image connectivity and therefore do not represent direct three-dimensional open and closed porosity measurements.
The pore phase was segmented using a grayscale threshold, followed by particle analysis to quantify the projected pore area, equivalent circular diameter, and circularity. Circularity was calculated according to , where is the projected pore area and is its perimeter, with values approaching 1 indicating more circular pores. Small features below the selected minimum particle area were excluded to reduce the influence of image noise. For the two-dimensional SEM images, pore regions connected to the image boundary were classified as apparent open pores, whereas enclosed segmented regions were classified as apparent closed pores. This classification describes apparent pore connectivity in the analyzed two-dimensional sections and should not be interpreted as a direct measurement of three-dimensional open and closed porosity. Accordingly, the percentages reported in Table 6 represent the fraction of segmented pore area classified as apparently open or enclosed within the analyzed SEM fields.
The quantitative image analysis supports the morphological differences observed in the SEM micrographs (Figure 8). BTG exhibited the largest median equivalent pore diameter (~4.7 µm) and relatively high mean circularity (~0.58), confirming the predominance of rounded and spheroidal pores observed in Figure 8a,b. This morphology is consistent with a higher degree of vitrification and pore spheroidization. The predominance of apparently enclosed pore regions (~93% of the segmented pore area) also supports the hypothesis that gas was retained within a viscous matrix during sintering.
In contrast, BTCL presented a substantially smaller median pore diameter (~0.9 µm) and lower circularity (~0.34), indicating a more irregular pore morphology. This result agrees with the interconnected and sharp-edged cavities observed in Figure 8c,d and is consistent with incomplete vitrification at 1100 °C. Such an irregular and connected pore structure is also consistent with the higher water absorption observed for this condition.
The BTSD sample showed a relatively uniform pore distribution, with a median equivalent diameter of approximately 4.5 µm and a mean circularity of ~0.54. These values quantitatively support the predominantly oval-to-spherical morphology observed in Figure 8e,f. The relatively high apparent closed-pore fraction (~96%) is consistent with the development of a more stabilized porous structure. For BF, the quantitative analysis indicated a smaller median pore diameter (~1.4 µm) and greater morphological heterogeneity, in agreement with the irregular pores and microfractures observed in Figure 8g,h.
Overall, the image analysis indicates that the mechanical and physical behavior of the aggregates is associated not only with the amount of porosity but also with pore morphology and apparent connectivity. Rounded, predominantly enclosed pores are expected to produce less severe stress concentration than irregular or interconnected cavities. However, because the present analysis is based on two-dimensional SEM images, the apparent open/closed pore fractions should be interpreted as indicators of surface connectivity rather than as direct measurements of three-dimensional open and closed porosity.
3.3. Environmental Performance of Lightweight Artificial Aggregates
Figure 9 and Figure 10 present the cumulative energy demand and global warming potential (GWP) throughout the life cycle, identifying key environmental hotspots and supporting the optimization of sustainable performance. The integrated analysis supports the assessment of trade-offs between energy efficiency and CO2 emissions, guiding decisions towards environmental optimization and greater sustainability.
Figure 9.
Life cycle cumulative energy demand by stage.
Figure 10.
Life cycle global warming potential by stage.
The calculated total energy demand of the developed mixtures ranged from 3890.50 to 5410.50 MJ/t, depending on PPR content and firing temperature, whereas the commercial expanded-clay reference (CC) presented a value of 5471.00 MJ/t. Because all values were calculated using the same functional basis of 1 tonne of lightweight aggregate and consistent system boundaries, the comparison provides an estimate of the relative energy performance of the developed formulations under the adopted industrial-scale scenario.
At 1100 °C, the residue-based formulations showed lower calculated energy demand than the commercial reference, with values of 3990.50 MJ/t for the 90% PPR formulation, 4050.50–4110.50 MJ/t for the 60% formulations, and 4110.50 MJ/t for the 30% formulation. As the firing temperature increased, the calculated energy demand also increased, reaching 4420.50–4540.50 MJ/t at 1150 °C and 4880.50–4980.50 MJ/t at 1200 °C. At 1250 °C, the values approached the commercial reference, ranging from 5070.50 to 5410.50 MJ/t.
These results indicate that, under the adopted industrial-scale calculation assumptions, higher PPR incorporation combined with moderate firing temperatures can reduce the calculated energy demand relative to the commercial expanded-clay reference. The magnitude of this difference, however, depends on the thermal-energy assumptions adopted for the industrial-scale scenario.
At the highest firing temperatures (1225–1250 °C), emissions approached the CC benchmark but did not surpass it. At 1225 °C, mixtures showed 279.73–287.53 kg CO2-eq/t, while at 1250 °C, values ranged from 292.05 to 299.85 kg CO2-eq/t, corresponding to reductions of approximately 1–8% relative to CC. The 60% and 30% formulations tended to present slightly higher emissions at elevated temperatures, whereas the 90% mixtures consistently maintained the lowest GWP across all thermal conditions.
The calculated GWP of the developed mixtures ranged from 219.25 to 299.85 kg CO2-eq/t, compared with 303.75 kg CO2-eq/t for the commercial expanded-clay reference. Using the same reference flow, system boundaries, and inventory assumptions, the developed formulations presented lower modeled GWP than the commercial expanded-clay reference. This result represents a comparative outcome of the modeled scenarios and should not be interpreted as direct evidence of lower industrial-scale emissions, because the thermal-energy requirements for the developed aggregates were estimated rather than measured in operating industrial kilns.
At 1100 °C, the 90% PPR formulations presented the lowest calculated GWP (219.25 kg CO2-eq/t), corresponding to approximately 27.8% lower impact than the commercial reference. As the firing temperature increased, the calculated GWP progressively increased, reaching 243.33–251.13 kg CO2-eq/t at 1150 °C and 267.97–275.77 kg CO2-eq/t at 1200 °C. At 1225–1250 °C, the calculated values approached the commercial reference, with reductions of approximately 1–8% at 1250 °C.
The results indicate that, within the adopted industrial-scale scenario, increasing PPR incorporation and controlling the sintering temperature are effective strategies for reducing the calculated GWP of the lightweight aggregates. These results should be interpreted in relation to the assumptions adopted for the industrial-scale energy inventory.
Overall, the results demonstrate that the optimal processing condition (~1150 °C) represents a transition between densification-controlled behavior and expansion-driven microstructure development. This balance ensures sufficient internal porosity for lightweight performance while preserving the mechanical strength required for structural applications.
An important limitation of the environmental comparison is that the thermal-energy requirements for the developed aggregates were modeled from laboratory-derived processing conditions rather than measured in industrial kilns. Industrial production may differ in terms of kiln efficiency, heat losses, residence time, heat recovery, loading conditions, and fuel utilization. Therefore, the absolute energy and GWP values reported here should not be interpreted as validated industrial performance indicators. Instead, the results provide a consistent comparative assessment of the investigated formulations under the same modeling framework. The thermal-energy sensitivity analysis further evaluates the extent to which the comparative results depend on the adopted energy assumptions. Direct industrial-scale measurements will be required to validate the absolute energy consumption and GWP values before commercial-scale environmental performance can be established.
3.4. Multi-Response Desirability Optimization
Table 7 presents the unified ANOVA, since the residual deviation was statistically insignificant and the same independent variables governed both response parameters. The assumptions of normality and homoscedasticity were met, and no structural differences were identified between the models. Therefore, consolidating the analysis into a single table preserves statistical robustness, avoids redundancy, and improves the clarity of the results.
Table 7.
Unified ANOVA for environmental performance and mechanical strength.
ANOVA shows that sintering temperature is the dominant and statistically significant factor (39.29% contribution; F = 9.73; p < 0.001). PPR content is also significant (18.27%; F = 9.05; p = 0.001), but with a smaller effect. In contrast, clay type has minimal influence (2.09%; p = 0.278) and is not significant. The high residual variance (40.36%) suggests that additional sources of variability, such as microstructural heterogeneity and stochastic pore formation, significantly influence the results. This variability underscores the need for cautious interpretation of peak mechanical values, particularly when they are associated with very low-density results. Accordingly, exceptionally high individual or mean mechanical values associated with very low density should be interpreted as observed experimental outcomes rather than as definitive intrinsic properties of the formulation, until independently reproduced using new batches.
The statistical models presented moderate coefficients of determination (R2 ≈ 0.60), indicating that the selected factors explain a substantial portion of the variability. The adjusted R2 values (≈0.57) were consistent with the R2 results, confirming that the model retains explanatory capability without overfitting. The relatively high residual contribution (40.36%) reflects the intrinsic variability associated with pore formation and microstructural evolution during sintering. Lightweight aggregate production involves stochastic mechanisms such as gas generation, entrapment, and pore coalescence, which are highly sensitive to local heterogeneities and are not fully captured by the main experimental variables. Despite this variability, the model remains statistically significant and suitable for identifying trends and supporting multi-response desirability optimization within the investigated experimental domain.
Although a formal lack-of-fit test was not performed, the residual diagnostics did not indicate an obvious systematic lack of fit within the investigated experimental domain. Therefore, the model was considered suitable for identifying general trends and supporting multi-response desirability optimization. However, its predictive accuracy for absolute values is inherently limited by the stochastic nature of microstructural evolution and the relatively high residual contribution observed in the ANOVA.
Figure 11 presents the interaction plots for total CO2 emissions and crush resistance, providing a graphical visualization of the combined response patterns associated with the investigated factors. These plots are intended for exploratory interpretation of factor combinations and do not represent formal statistical tests of interaction significance.
Figure 11.
Full interaction effect plots: (a) Total CO2 emissions (kg CO2-eq/t). (b) Crush resistance (MPa).
The results demonstrate that the global warming potential (GWP) is strongly governed by the sintering temperature, increasing consistently from 1100 to 1250 °C, indicating that thermal processing energy consumption constitutes the primary environmental hotspot of the system. In contrast, raising the PPR content from 30 to 90% results in a systematic reduction in GWP, suggesting a mitigating effect from partial replacement of conventional raw materials and/or lower embodied energy. Differences among clay types are marginal under all conditions, showing that mineralogical formulation has a secondary environmental impact compared with processing parameters. Thus, environmental optimization of the material primarily depends on controlling the sintering temperature. At the same time, PPR incorporation emerges as an effective complementary strategy to reduce the production cycle’s carbon footprint.
The results indicate that mechanical strength is jointly influenced by composition and processing conditions, with sintering temperature emerging as the dominant factor. Strength increases markedly from 1100 °C to approximately 1150–1200 °C, where peak values are observed, followed by stabilization or a slight decline at higher temperatures, suggesting an optimal densification window beyond which microstructural coarsening or pore evolution may offset gains. Increasing PPR content generally enhances strength, particularly at intermediate temperatures, indicating a beneficial role in promoting particle packing or reactive bonding. Differences among clay formulations are noticeable but secondary, with certain compositions consistently outperforming others under identical conditions. Overall, these findings demonstrate that maximizing mechanical performance requires a balanced optimization of thermal treatment and additive content, rather than adjusting a single parameter.
Table 8 presents the results of the multi-response desirability optimization, simultaneously minimizing total CO2 emissions and maximizing crush resistance, thereby identifying the processing condition that provides the best balance between mechanical performance and environmental sustainability within the investigated experimental domain.
Table 8.
Multi-response desirability optimization of mechanical and environmental performance.
A weighting sensitivity analysis was performed to assess the influence of the relative weighting assigned to mechanical and environmental performance on the identified optimum. The analysis considered weighting scenarios of 25/75, 50/50, and 75/25 for mechanical strength and CO2-equivalent emissions, respectively. This analysis is distinct from the thermal-energy sensitivity analysis described in Section Thermal-Energy Sensitivity Analysis, which evaluates the influence of the assumed process-energy requirements on the environmental indicators.
The sensitivity analysis showed that the optimal PPR content remained stable at 90% across all weighting scenarios, whereas the optimal sintering temperature was sensitive to the relative importance assigned to environmental performance. When mechanical strength and CO2 emissions were equally weighted (50/50), the optimum was BTCL with 90% PPR sintered at 1150 °C. Increasing the weight assigned to CO2 emissions to 75% shifted the optimum to 90% PPR and 1100 °C, whereas increasing the weight assigned to mechanical strength to 75% maintained the optimum at 90% PPR and 1150 °C. These results indicate that the selected optimum is robust with respect to PPR incorporation, while the optimal sintering temperature depends to some extent on the relative weighting of mechanical and environmental performance. Therefore, BTCL–90% PPR–1150 °C represents the preferred compromise under the adopted equal-weight criterion, whereas a stronger preference for environmental performance favors the lower sintering temperature of 1100 °C.
The results demonstrate that the multi-response desirability optimization is effective in identifying sustainable processing conditions within the investigated experimental domain, providing quantitative guidelines for balancing mechanical performance and CO2 emissions. Figure 12 presents the desirability graph for the simultaneous optimization of responses, highlighting the operational region that maximizes compressive strength while minimizing total CO2 emissions.
Figure 12.
Desirability plot for simultaneous optimization of compressive strength and total CO2 emissions.
The global optimum point (D = 0.7432) corresponds to the combination of BTCL clay, 90% PPR, and a sintering temperature of 1150 °C, highlighted by the red vertical lines, indicating the best compromise between mechanical performance and environmental impact. Under this condition, a predicted strength of 22.38 MPa is observed, associated with emissions of 243.36 kg CO2-eq/t, values that simultaneously represent the maximum and minimum desired for each response. The distribution of experimental points shows a consistent trend of responses with the factors, confirming the robustness of the model and the stability of the identified optimum. Taken together, the results demonstrate that the multi-response desirability approach is effective in defining sustainable processing windows, providing quantitative guidelines for the design of high-performance, low-carbon footprint materials.
Under the equal-weight desirability criterion, all optimal solutions converged to 90% PPR and a sintering temperature of 1150 °C, while the clay type determined the final ranking through its effect on mechanical performance. The total CO2 emissions were essentially equivalent among the optimized solutions (243.36 kg CO2-eq/t). Consequently, the differentiation among clay types was primarily associated with their predicted crush resistance.
BTCL presented the highest composite desirability (D = 0.7432), with a predicted crush resistance of 22.38 MPa and total CO2 emissions of 243.36 kg CO2-eq/t. The corresponding experimental result confirmed the predicted optimum, with a measured crush resistance of 22.11 MPa and total CO2 emissions of 243.36 kg CO2-eq/t. These results indicate that the identified condition represents the best compromise within the investigated experimental domain under the adopted equal-weight criterion.
4. Conclusions
This study demonstrates the feasibility of producing lightweight aggregates with characteristics compatible with structural requirements, achieving properties consistent with those specified in ASTM C330/C330M [17]. The results agree with previous studies, including those by [6,16,21,28,36], providing indirect validation of their applicability to structural lightweight concrete. Statistical analysis (ANOVA) confirmed that sintering temperature is the most influential parameter governing overall performance, followed by residue content, while clay type showed no statistically significant effect.
Multi-response desirability optimization identified BTCL with 90% PPR sintered at 1150 °C as the preferred optimal condition within the investigated experimental domain under the adopted equal-weight desirability criterion, providing the best balance between mechanical strength and environmental impact. The sensitivity analysis showed that the optimum PPR content remained stable at 90% across the evaluated weighting scenarios, while the preferred sintering temperature shifted to 1100 °C when greater importance was assigned to CO2 reduction. This indicates that the selected BTCL–90% PPR–1150 °C condition is robust under balanced and mechanically oriented weighting, whereas a stronger environmental preference favors a lower sintering temperature.
From an environmental perspective, the modeled production scenarios indicated lower calculated energy demand and GWP for several residue-based lightweight aggregate formulations compared with the commercial expanded-clay reference under the adopted reference flow, system boundaries, and inventory assumptions. However, these results should not be interpreted as direct measurements or validated predictions of industrial kiln performance, because the thermal-energy requirements were estimated from laboratory-derived processing conditions. The thermal-energy sensitivity analysis evaluated the extent to which the calculated environmental indicators depend on these assumptions. Therefore, the environmental advantage identified in this study should be understood as a comparative result within the modeled scenarios, while industrial-scale validation through direct measurements of fuel consumption, kiln efficiency, heat recovery, and production losses remains necessary.
Therefore, the developed materials demonstrate strong potential as lightweight aggregates for structural concrete applications, based on their density, water absorption, expansion, and mechanical performance at the aggregate scale. Nevertheless, this classification remains preliminary because concrete-scale testing was not performed. Future studies should evaluate the incorporation of these developed aggregates into concrete mixtures, investigating fresh and hardened properties, aggregate-cement paste interaction, compressive strength, density, dimensional stability, and durability. Such testing will be necessary to establish the actual structural lightweight concrete performance of the developed aggregates.
Author Contributions
Conceptualization, K.S.d.C.L.V., J.A.d.S.N. and R.P.S.D.; methodology, K.S.d.C.L.V., J.P.d.C.L.V., L.L.d.S., and J.A.d.S.N.; validation, K.S.d.C.L.V., L.L.d.S., J.A.d.S.N. and C.M.P.; formal analysis, K.S.d.C.L.V., J.P.d.C.L.V., L.L.d.S. and J.A.d.S.N.; investigation, K.S.d.C.L.V., J.P.d.C.L.V. and J.A.d.S.N.; resources, K.S.d.C.L.V., J.A.d.S.N. and R.P.S.D.; data curation, J.P.d.C.L.V., L.L.d.S., J.A.d.S.N. and C.M.P.; writing—original draft preparation, K.S.d.C.L.V. and J.P.d.C.L.V.; writing—review and editing, L.L.d.S., J.A.d.S.N., C.M.P. and R.P.S.D.; visualization, J.P.d.C.L.V. and L.L.d.S.; supervision, R.P.S.D.; project administration: R.P.S.D. All authors have read and agreed to the published version of the manuscript.
Funding
This research received no external funding.
Data Availability Statement
The original contributions presented in this study are included in the article. Further inquiries can be directed to the corresponding author.
Acknowledgments
The authors thank the Federal University of Paraíba (UFPB) for its institutional support and for providing the laboratory infrastructure of the Ceramic Materials Laboratory (LMC-UFPB), which was essential for the development of this research.
Conflicts of Interest
The authors declare no conflicts of interest.
References
- Tam, V.W.Y.; Soomro, M.; Evangelista, A.C.J. A Review of Recycled Aggregate in Concrete Applications (2000–2017). Constr. Build. Mater. 2018, 172, 272–292. [Google Scholar] [CrossRef] [Scilit]
- Dos Santos, K.; Figueirêdo, A.; De Paiva, D.; Maia, F.L.; Da Silva, J.A.; Da Silva, I.M.; Costa, I. Fresh, hardened, and thermal properties of coating mortars containing mineral additions and vermiculite. Mater. Constr. 2023, 73, e318. [Google Scholar] [CrossRef] [Scilit]
- Le Bissonnais, Y. Soil Characteristics and Aggregate Stability. In Soil Erosion, Conservation, and Rehabilitation; CRC Press: Boca Raton, FL, USA, 2023; pp. 41–60. [Google Scholar]
- Cooke, S.J.; Piczak, M.L.; Nyboer, E.A.; Michalski, F.; Bennett, A.; Koning, A.A.; Hughes, K.A.; Chen, Y.; Wu, J.; Cowx, I.G. Managing Exploitation of Freshwater Species and Aggregates to Protect and Restore Freshwater Biodiversity. Environ. Rev. 2023, 32, 414–437. [Google Scholar] [CrossRef] [Scilit]
- Sabău, M.; Bompa, D.V.; Silva, L.F.O. Comparative Carbon Emission Assessments of Recycled and Natural Aggregate Concrete: Environmental Influence of Cement Content. Geosci. Front. 2021, 12, 101235. [Google Scholar] [CrossRef] [Scilit]
- Silva Neto, J.A.; Cavalcante, D.S.L.; Medeiros, C.M.; Anjos, M.A.S.; Dutra, R.P.S.; Souza, M.M.; Pederneiras, C.M.; Silva Mateus, R.F.M. Development of artificial lightweight aggregates with chamotte and eucalyptus firewood ash residues: Life cycle assessment and economic feasibility. Constr. Build. Mater. 2025, 504, 144600. [Google Scholar] [CrossRef] [Scilit]
- De Silva, G.H.M.J.S.; Hansamali, E. Eco-Friendly Fired Clay Bricks Incorporated with Porcelain Ceramic Sludge. Constr. Build. Mater. 2019, 228, 116754. [Google Scholar] [CrossRef] [Scilit]
- Samadi, M.; Fahim, G.; Mohammadhosseini, H.; Alyousef, R. Waste Ceramic as Low Cost and Eco-Friendly Materials in the Production of Sustainable Mortars. J. Clean. Prod. 2020, 266, 121825. [Google Scholar] [CrossRef] [Scilit]
- Almeida, E.P.; Carreiro, M.E.A.; Rodrigues, A.M.; Ferreira, H.S.; Santana, L.N.L.; Menezes, R.; Neves, G.A. A New Eco-Friendly Mass Formulation Based on Industrial Mining Residues for the Manufacture of Ceramic Tiles. Ceram. Int. 2021, 47, 11340–11348. [Google Scholar] [CrossRef] [Scilit]
- Bernhardt, M.; Tellesbø, H.; Justnes, H.; Wiik, K. Mechanical Properties of Lightweight Aggregates. J. Eur. Ceram. Soc. 2013, 33, 2731–2743. [Google Scholar] [CrossRef] [Scilit]
- Azam, F.A.; Shamsudin, R.; Ng, M.H.; Zainuddin, Z.; Hamid, M.A.A.; Rashid, R.A. Mechanical and Bioactive Properties of Mullite Reinforced Pseudowollastonite Biocomposite. Sains Malays 2018, 47, 2141–2149. [Google Scholar] [CrossRef] [Scilit]
- Taheri, S.; Delgado, G.P.; Agbaje, O.B.A.; Giri, P.; Clark, S.M. Corrosion Inhibitory Effects of Mullite in Concrete Exposed to Sulfuric Acid Attack. Corros. Mater. Degrad. 2020, 1, 14. [Google Scholar] [CrossRef] [Scilit]
- Nair, N.A.; Sairam, V. Research Initiatives on the Influence of Wollastonite in Cement-Based Construction Material—A Review. J. Clean. Prod. 2021, 283, 124665. [Google Scholar] [CrossRef] [Scilit]
- Bekkeri, G.B.; Shetty, K.K.; Nayak, G.; Dafedar, M.M.M.; Jambhale, N.A.; Sachin, K.C. Waste-Derived Artificial Aggregates for Concrete Applications. Mater. Res. Express 2025, 12, 85306. [Google Scholar] [CrossRef] [Scilit]
- Abuqasim, S.; Ersoy, S.; Kurtay-Yildiz, M.; Öztürk, İ.Ş.; Sari, F.A.; Emiroğlu, M. Examination of Porcelain Polishing Residue as a Supplementary Cementitious Materials. J. Build. Eng. 2025, 109, 112897. [Google Scholar] [CrossRef] [Scilit]
- Martins De Oliveira, V.S.; Neto, J.A.D.S.; Nascimento, G.L.D.; Anjos, M.A.S.D.; Dutra, R.P.S.; Pederneiras, C.M. Evaluating porcelain polishing waste as a pyro-expansive agent in clay formulations for sustainable lightweight aggregates. Sustainability 2025, 17, 7385. [Google Scholar] [CrossRef] [Scilit]
- ASTM C330/C330M-14; Standard Specification for Lightweight Aggregates for Structural Concrete. In ASTM Volume 04.02: Concrete and Aggregates. ASTM International: West Conshohocken, PA, USA, 2014.
- Silva, R.H.L.; Neves, G.A.; Nóbrega, A.C.V.; Farias, R.M.C.; Rocha, M.F.B.; Alves, K.G.B.; Menezes, R.R. Effect of the Addition of Porcelain Tile Polishing Residue in Ceramic Masses for Sanitary Ware. Mater. Res. 2023, 26, e20230563. [Google Scholar] [CrossRef] [Scilit]
- Jacoby, P.C.; Pelisser, F. Pozzolanic Effect of Porcelain Polishing Residue in Portland Cement. J. Clean. Prod. 2015, 100, 84–88. [Google Scholar] [CrossRef] [Scilit]
- de Souza Santos, P. Industrial Clays in Brazil: A Review. In 2001. A Clay Odyssey; Elsevier: Amsterdam, The Netherlands, 2003; Volume 1, p. 323. [Google Scholar]
- Da Silva Neto, J.A.; dos Anjos, M.A.S.; Dutra, R.P.S.; Mendonça de Souza, M.; Pederneiras, C.M. Development of Sustainable Artificial Lightweight Aggregates with Binary Mixtures of Waste Rich in Aluminosilicate and Carbonate in Kaolinitic Clay. Sustainability 2025, 17, 2017. [Google Scholar] [CrossRef] [Scilit]
- Chen, H.-J.; Chen, P.-C.; Peng, C.-F.; Huang, C.-W. Production of synthetic lightweight aggregates from industrial sludge. Materials 2022, 15, 4097. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Li, X.; Liu, W.; Li, L.; Liu, X.; Li, X.; Guo, S.; Xu, W.; Xu, W.; Guo, J.; Wang, H.; et al. Energy efficient sintering of high-performance ceramics. J. Adv. Ceram. 2025, 14, 9221186. [Google Scholar] [CrossRef] [Scilit]
- Kong, Y.Y.S.; Wang, Q.; Lu, J.-X.; Poon, C.S. Lightweight aggregates produced from low-temperature sintering of multiple solid wastes for heavy metals removal: Adsorption kinetics and stabilization. J. Clean. Prod. 2024, 480, 144118. [Google Scholar] [CrossRef] [Scilit]
- Zhou, X.; Zhang, Y.; Liu, C.; Wu, F. Resource recovery of sludge incineration residue in lightweight aggregate: Performance mechanism, and environmental safety analysis. Constr. Build. Mater. 2024, 436, 136962. [Google Scholar] [CrossRef] [Scilit]
- Uceda-Rodríguez, M.; Moreno-Maroto, J.M.; Cobo-Ceacero, C.J.; López-García, A.B.; Cotes-Palomino, T.; Martínez-García, C. Comparative life cycle assessment of lightweight aggregates made from waste—Applying the circular economy. Appl. Sci. 2022, 12, 1917. [Google Scholar] [CrossRef] [Scilit]
- Silva, I.A.; Pereira, I.D.S.; Cavalcanti, W.S.; Sousa, F.K.A.; Neves, G.A.; Ferreira, H.C. Study of the Characterization of Smectitic Clays from a Town in the State of Paraíba. Mater. Sci. Forum 2015, 820, 51–55. [Google Scholar] [CrossRef] [Scilit]
- EN 13055-1:2002; Lightweight Aggregates-Part 1: Lightweight Aggregates for Concrete, Mortar and Grout. British Standard Institution: London, UK, 2002.
- NBR 7180; Soil—Determination of the Plasticity Limit. Brazilian Association of Technical Standards (ABNT): Rio de Janeiro, Brazil, 2016.
- NBR 6459; Soil—Determination of the Liquid Limit. Brazilian Association of Technical Standards (ABNT): Rio de Janeiro, Brazil, 2025.
- Huang, C.-H.; Wang, S.-Y. Application of Water Treatment Sludge in the Manufacturing of Lightweight Aggregate. Constr. Build. Mater. 2013, 43, 174–183. [Google Scholar] [CrossRef] [Scilit]
- Li, B.; Ling, T.-C.; Qu, L.; Wang, Y. Effects of a Two-Step Heating Process on the Properties of Lightweight Aggregate Prepared with Sewage Sludge and Saline Clay. Constr. Build. Mater. 2016, 114, 119–126. [Google Scholar] [CrossRef] [Scilit]
- BR NM 16917; Coarse Aggregate—Determination of Specific Mass, Apparent Specific Mass and Water Absorption. Brazilian Association of Technical Standards (ABNT): Rio de Janeiro, Brazil, 2021.
- ACI 213 R-03; Guide for Structural Lightweight Aggregate Concrete. American Concrete Institute: Farmington Hills, MI, USA, 2003.
- NBR NM 16972; Aggregates—Determination of Unit Mass and Void Index. Brazilian Association of Technical Standards (ABNT): Rio de Janeiro, Brazil, 2021.
- Da Silva Neto, J.A.; Dos Anjos, M.A.S.; Dutra, R.P.S.; Mendonça De Souza, M.; Pederneiras, C.M. Optimization via taguchi of artificial lightweight aggregates obtained from kaolinite clay and ceramic waste: Development and industrial applications. Buildings 2025, 15, 2003. [Google Scholar] [CrossRef] [Scilit]
- Betioli, A.M.; Fortunato, M.; Martins, B.H.; Casali, J.M.; Rocha, J.C.; Collodetti, G. Effects of Particle Size and Specific Surface Area of Porcelain Tile Polishing Waste on Selfcompacting Mortars. J. Build. Technol. 2024, 6, 385–402. [Google Scholar] [CrossRef] [Scilit]
- Rambaldi, E.; Esposito, L.; Tucci, A.; Timellini, G. Recycling of Polishing Porcelain Stoneware Residues in Ceramic Tiles. J. Eur. Ceram. Soc. 2007, 27, 3509–3515. [Google Scholar] [CrossRef] [Scilit]
- ISO 14040:2006; Environmental Management—Life Cycle Assessment—Principles and Framework. International Organization for Standardization (ISO): Geneva, Switzerland, 2006.
- ISO 14044:2006; Environmental Management—Life Cycle Assessment—Requirements and Guidelines. International Organization for Standardization (ISO): Geneva, Switzerland, 2006.
- Sistema de Informações Sobre Desempenho Ambiental da Construção (SIDAC). Sistema de Informação do Desempenho Ambiental da Construção. Available online: https://sidac.org.br/ (accessed on 14 February 2026).
- CINEXPAN, Expanded Clay. Technical Data Sheet Type 3222.pdf. Available online: https://www.cinexpan.com.br/pdf/ficha-tecnica-tipo-3222.pdf (accessed on 27 January 2026).
- CINEXPAN, Expanded Clay. Technical Data Sheet Type 2215.pdf. Available online: https://www.cinexpan.com.br/pdf/ficha-tecnica-tipo-2215.pdf (accessed on 27 January 2026).
- CINEXPAN, Expanded Clay. Technical Data Sheet Type 1506.pdf. Available online: https://www.cinexpan.com.br/pdf/ficha-tecnica-tipo-1506.pdf (accessed on 27 January 2026).
- IPCC. Climate Change 2013: The Physical Science Basis; Contribution of Working Group I to the Fifth Assessment Report of the Intergovernmental Panel on Climate Change; Cambridge University Press: Cambridge, UK, 2013. [Google Scholar] [CrossRef] [Scilit]
- Sampaio, Z.L.M.; Martinelli, A.E.; Gomes, T.S. Formulation and Characterization of Structural Lightweight Concrete Containing Residues of Porcelain Tile Polishing, Tire Rubber and Limestone. Cerâmica 2017, 63, 530–535. [Google Scholar] [CrossRef] [Scilit]
- Garboczi, E.J.; Riding, K.A.; Mirzahosseini, M. Particle Shape Effects on Particle Size Measurement for Crushed Waste Glass. Adv. Powder Technol. 2017, 28, 648–657. [Google Scholar] [CrossRef] [Scilit]
- Emmerich, K.; Wolters, F.; Kahr, G.; Lagaly, G. Clay Profiling: The Classification of Montmorillonites. Clays Clay Miner. 2009, 57, 104–114. [Google Scholar] [CrossRef] [Scilit]
- Caldas-Vieira, F.; Feuerborn, H.-J.; Saraber, A. European Product Standards—Update on Status and Changes with Relevance to CCPs. In Proceedings of the 2013 World of Coal Ash (WOCA) Conference, Lexington, KY, USA, 22–25 April 2013. [Google Scholar]
- dos Santos Conserva, L.R.; Melchiades, F.G.; Nastri, S.; Boschi, A.O.; Dondi, M.; Guarini, G.; Raimondo, M.; Zanelli, C. Pyroplastic Deformation of Porcelain Stoneware Tiles: Wet vs. Dry Processing. J. Eur. Ceram. Soc. 2017, 37, 333–342. [Google Scholar] [CrossRef] [Scilit]
- Sánchez, E.; Sanz, V.; Cañas, E.; Sales, J.; Kayacı, K.; Taşkıran, M.U.; Anıl, Ü.E.; Türk, Ş. Revisiting Pyroplastic Deformation. Application for Porcelain Stoneware Tile Bodies. J. Eur. Ceram. Soc. 2019, 39, 601–609. [Google Scholar] [CrossRef] [Scilit]
- Kwek, S.Y.; Awang, H. Utilization of Industrial Waste Materials for the Production of Lightweight Aggregates: A Review. J. Sustain. Cem. Mater. 2021, 10, 353–381. [Google Scholar] [CrossRef] [Scilit]
- Romero, M.; Padilla, I.; Contreras, M.; López-Delgado, A. Mullite-Based Ceramics from Mining Waste: A Review. Minerals 2021, 11, 332. [Google Scholar] [CrossRef] [Scilit]
- Xu, H.; Li, D.; Wang, Z.; Song, P.; Zhao, Y.; Su, H. Mullite-Based Abrasives for Chemical Mechanical Polishing of Silicon Carbide. Appl. Surf. Sci. 2025, 692, 162714. [Google Scholar] [CrossRef] [Scilit]
- Derkowski, A.; Kuligiewicz, A. Thermal Analysis and Thermal Reactions of Smectites: A Review of Methodology, Mechanisms, and Kinetics. Clays Clay Miner. 2022, 70, 946–972. [Google Scholar] [CrossRef] [Scilit]
- Zhou, H.; Brooks, A.L. Thermal and Mechanical Properties of Structural Lightweight Concrete Containing Lightweight Aggregates and Fly-Ash Cenospheres. Constr. Build. Mater. 2019, 198, 512–526. [Google Scholar] [CrossRef] [Scilit]
- Garzón, E.; Pérez-Villarejo, L.; Eliche-Quesada, D.; Martínez-Martínez, S.; Sanchez-Soto, P.J. Vitrification Rate and Estimation of the Optimum Firing Conditions of Ceramic Materials from Raw Clays: A Review. Ceram. Int. 2022, 48, 15889–15898. [Google Scholar] [CrossRef] [Scilit]
- Candeias, C.; Novo, S.; Rocha, F. Exploring Residual Clays for Low-Impact Ceramics: Insights from a Portuguese Ceramic Region. Appl. Sci. 2025, 15, 8761. [Google Scholar] [CrossRef] [Scilit]
- Molinari, C.; Zanelli, C.; Guarini, G.; Dondi, M. Bloating Mechanism in Lightweight Aggregates: Effect of Processing Variables and Properties of the Vitreous Phase. Constr. Build. Mater. 2020, 261, 119980. [Google Scholar] [CrossRef] [Scilit]
- Kumar, A.; Lingfa, P. Sodium Bentonite and Kaolin Clays: Comparative Study on Their FT-IR, XRF, and XRD. Mater. Today Proc. 2020, 22, 737–742. [Google Scholar] [CrossRef] [Scilit]
- Khan, H.; Ahmad, J.; Zahid, Z.B.; Irfan, S.; Umer, M. Development of Extrusion Based Artificial Lightweight Aggregates from Sand-Plastic Waste Composite for Sustainable Concrete Production: Performance Evaluation and Life Cycle Assessment. Case Stud. Constr. Mater. 2025, 22, e04663. [Google Scholar] [CrossRef] [Scilit]
- Shang, X.; Li, Z.; Chang, J.; Chen, Y.; Yang, J.; Duan, Z. Production, Properties and Life Cycle Assessment of Artificial Lightweight Aggregates Produced with Corn Straw Ash (CSA) and Concrete Slurry Waste (CSW). Constr. Build. Mater. 2024, 411, 134274. [Google Scholar] [CrossRef] [Scilit]
- Pontes, I.C.; Neto, J.A.D.S.; Lemos, M.H.C.; Anjos, M.A.S.D.; Pederneiras, C.M.; Dutra, R.P.S. Effect of high levels of pyroexpansive agents from porcelain polishing waste on artificial lightweight aggregates produced with red clay. Buildings 2026, 16, 940. [Google Scholar] [CrossRef] [Scilit]
- Huang, X.; Zhang, F.; Ma, X.; Onn, C.C.; Lim, Y.P.; Lim, H.K.; Tan, C.Y.; Mo, K.H. Role of waste glass as a fluxing agent in the sintering mechanism of porous ceramic aggregates from aluminium dross. J. Eur. Ceram. Soc. 2025, 45, 117587. [Google Scholar] [CrossRef] [Scilit]
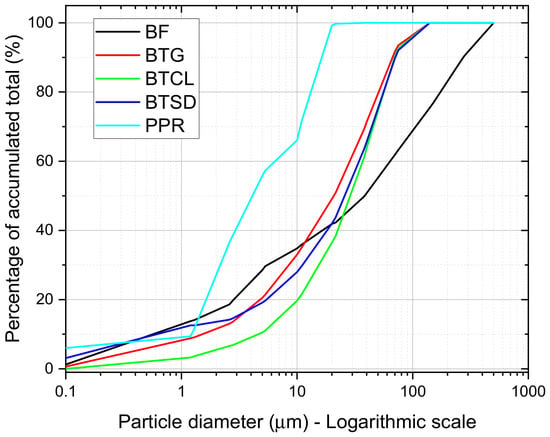
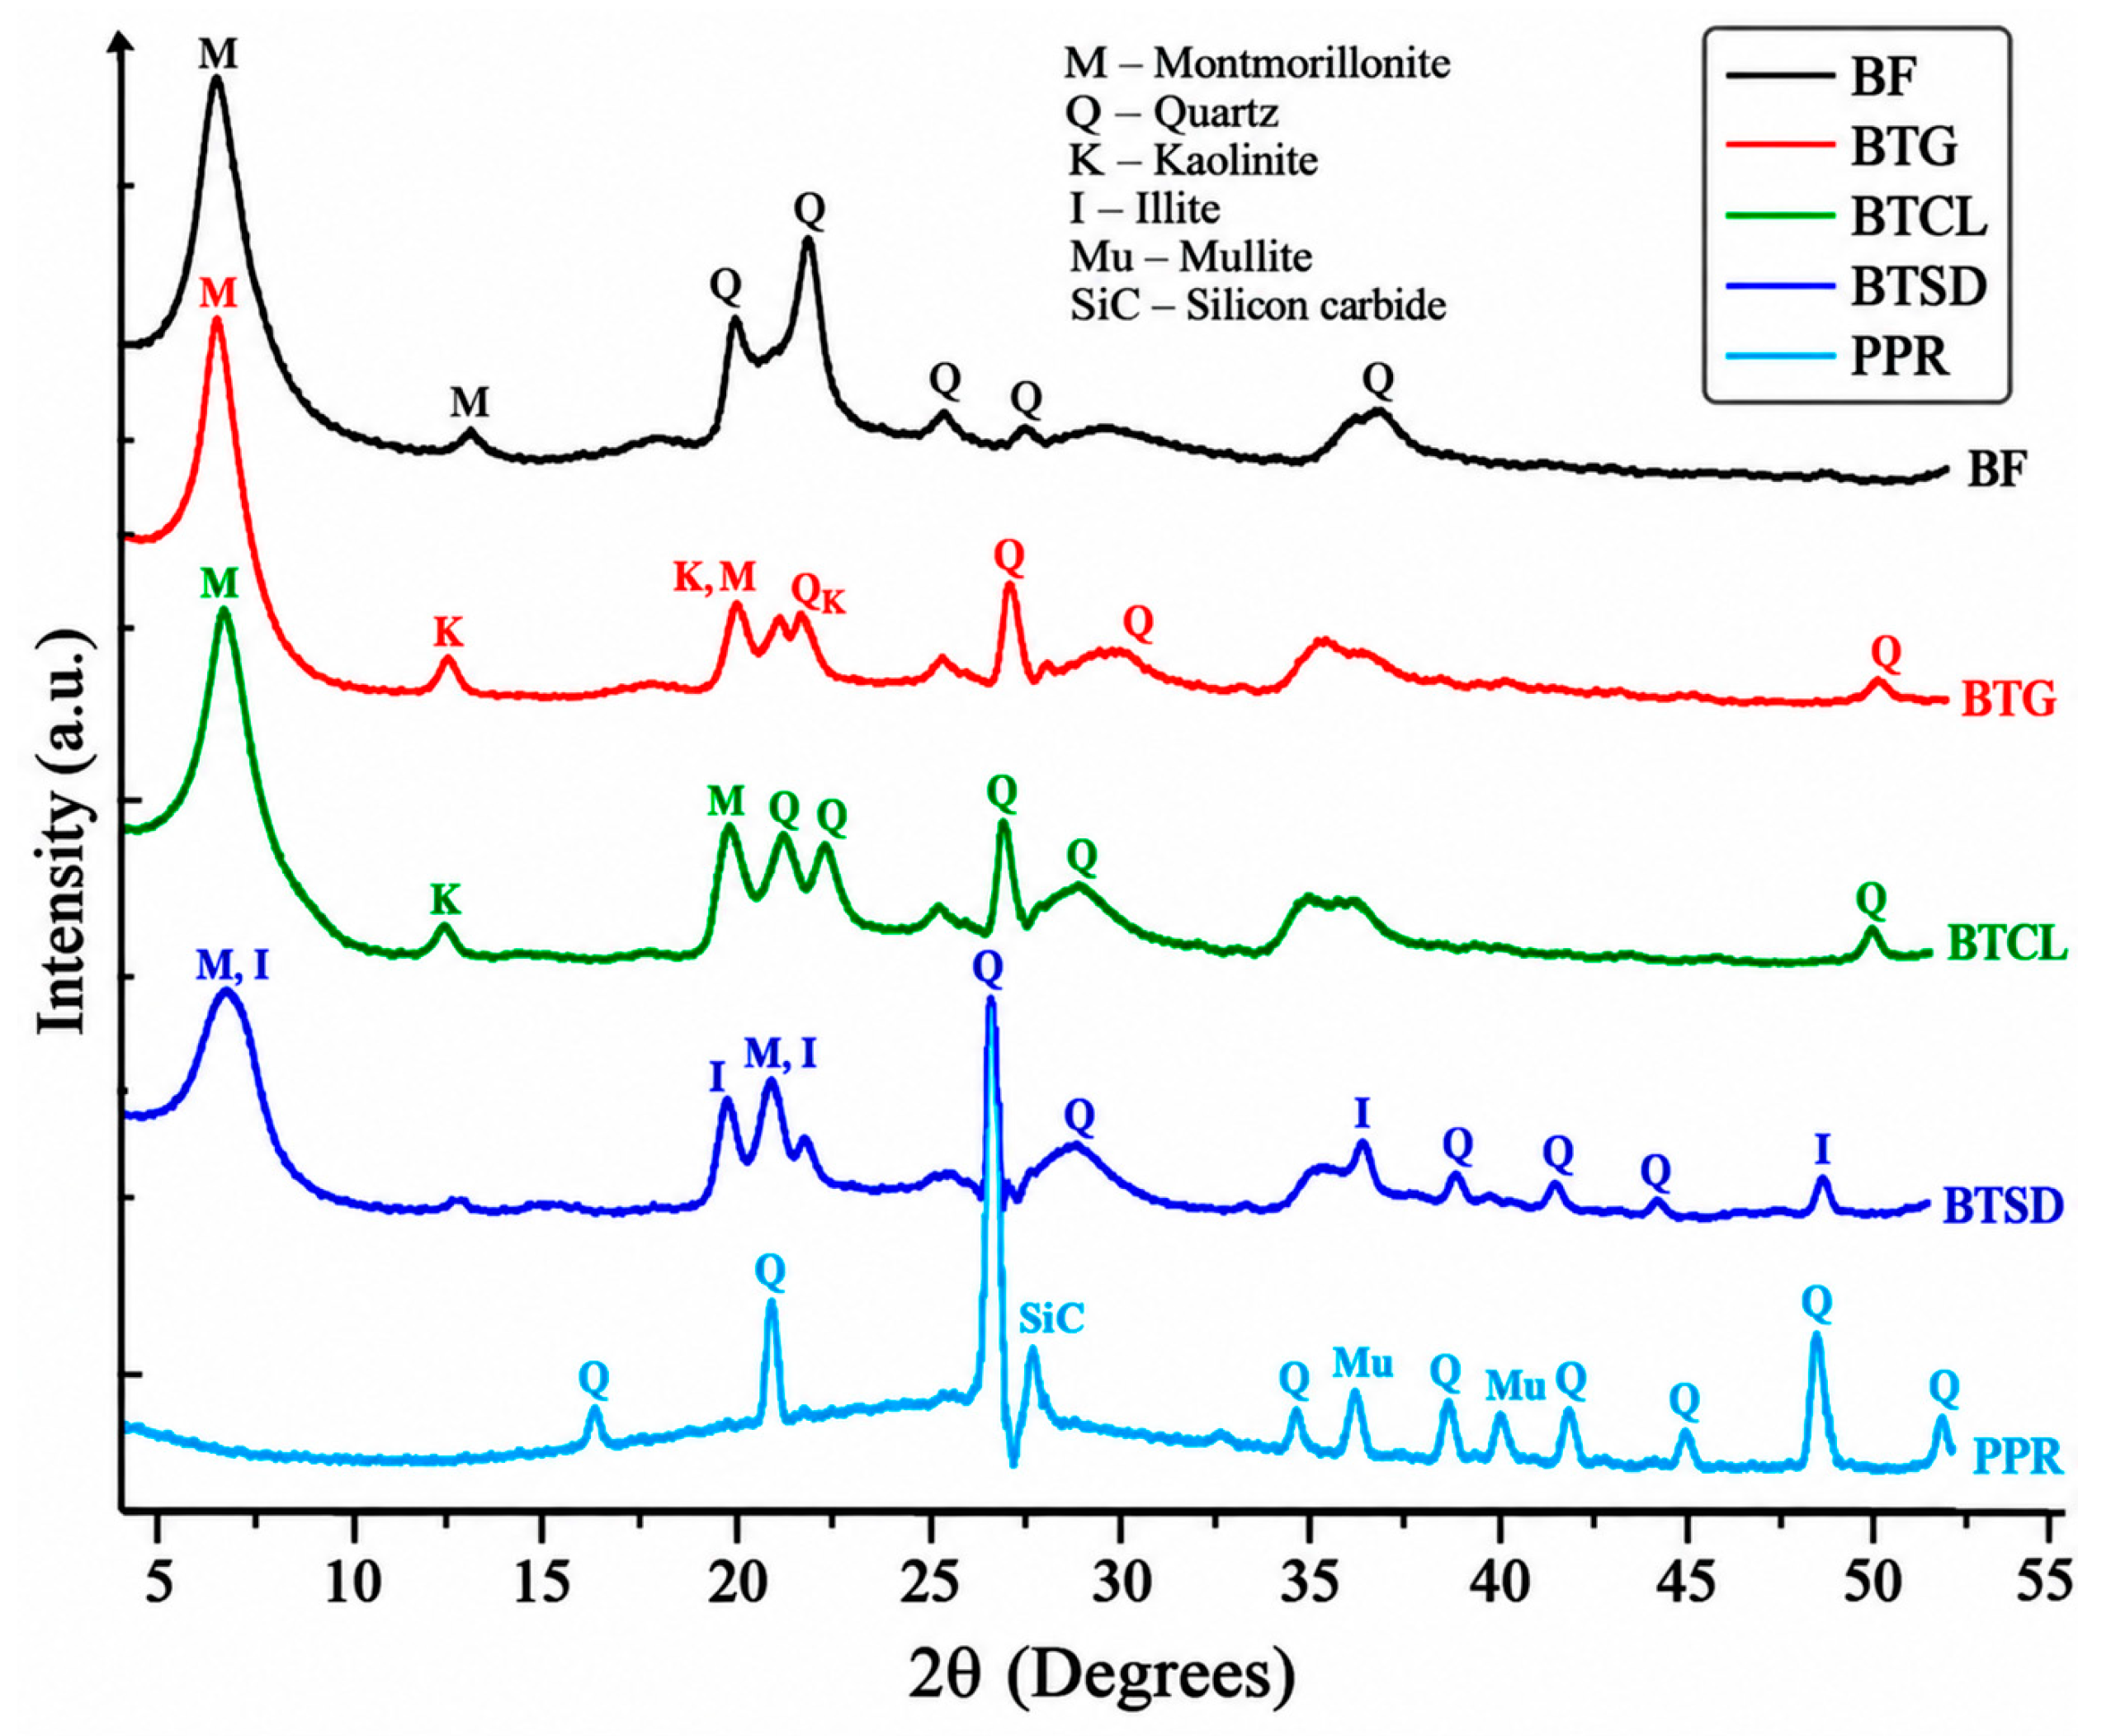
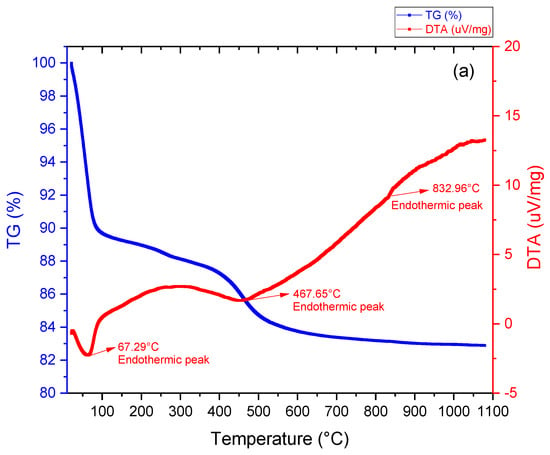
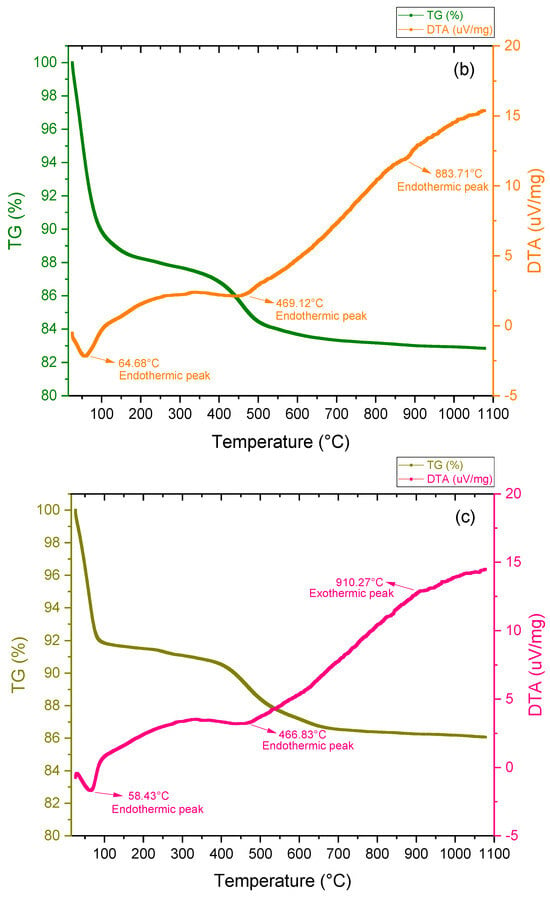
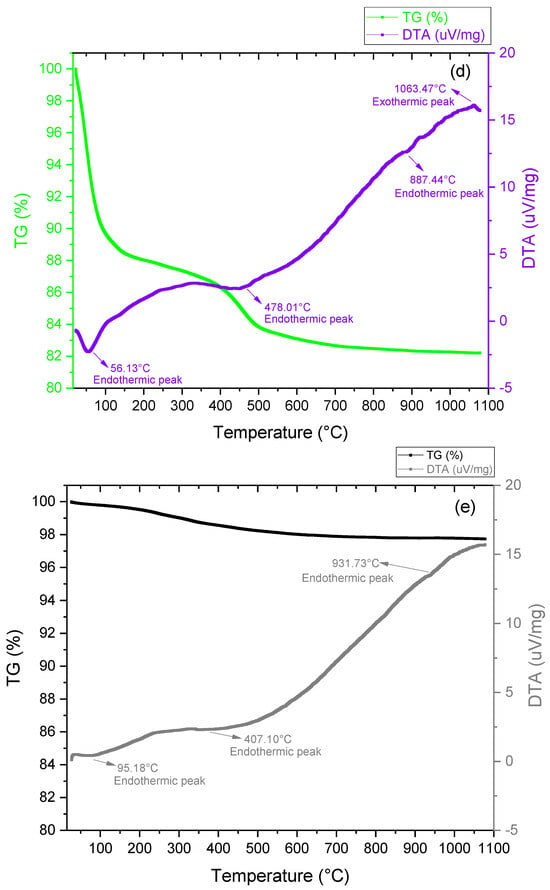
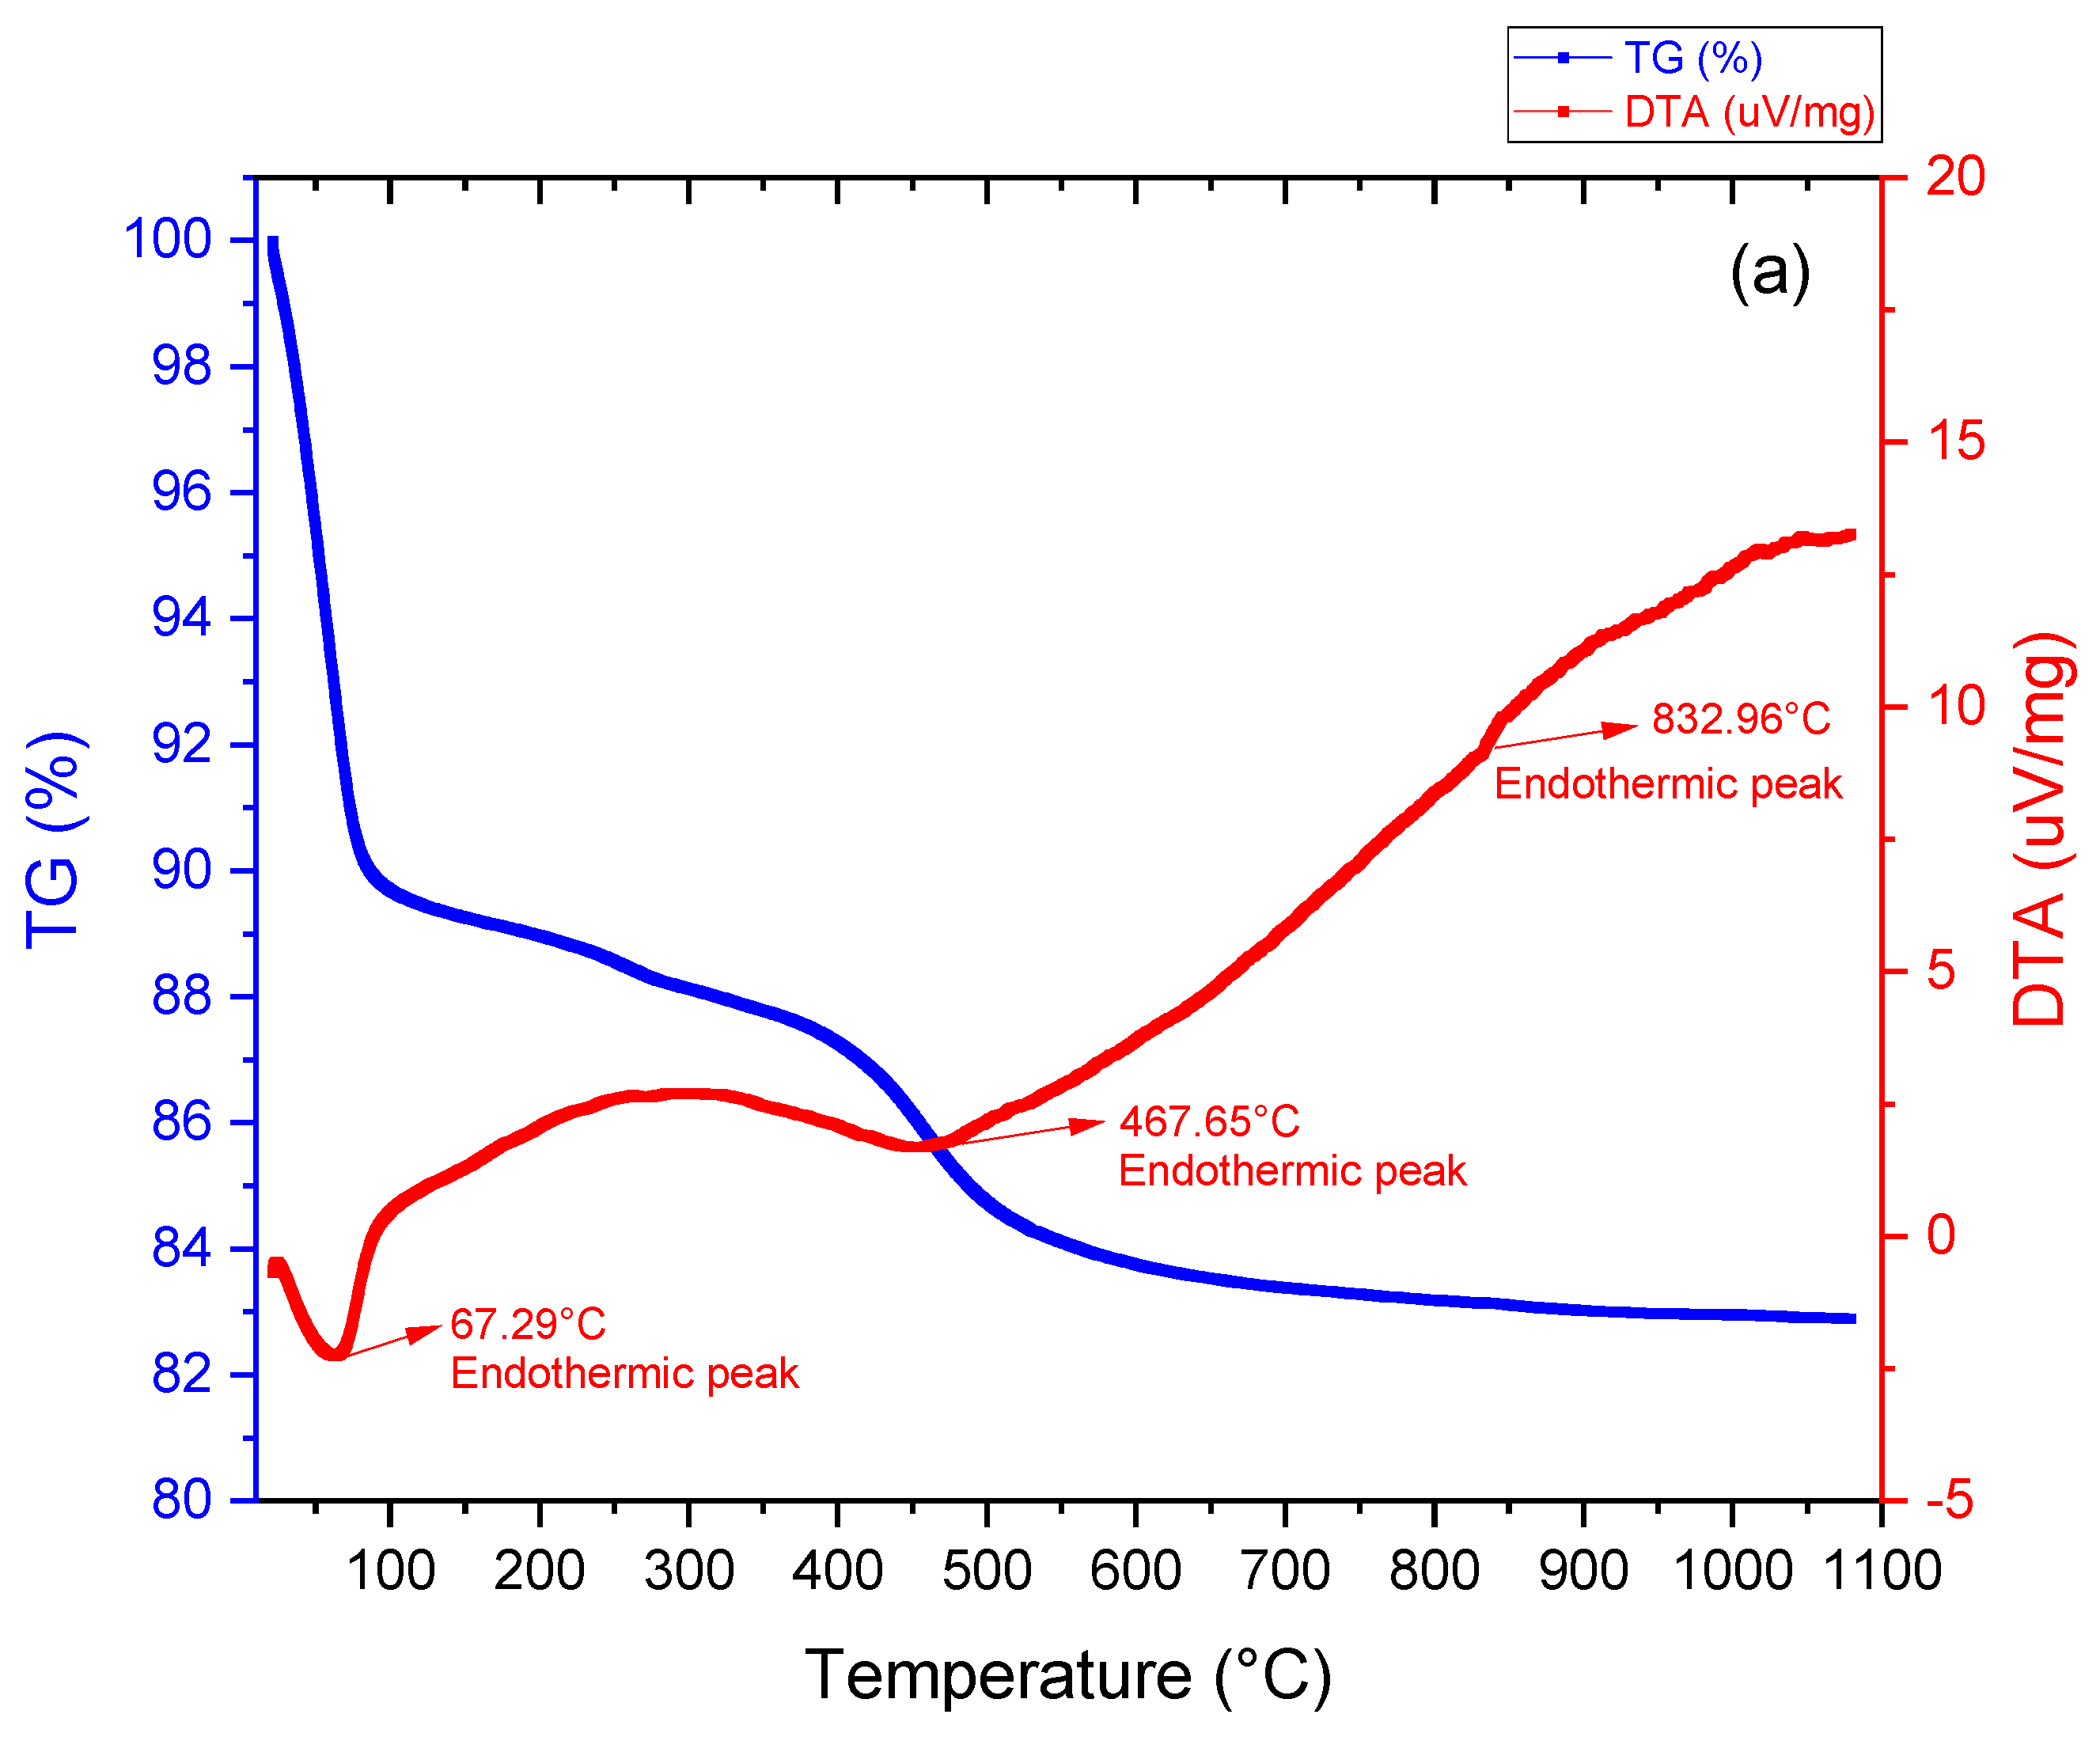
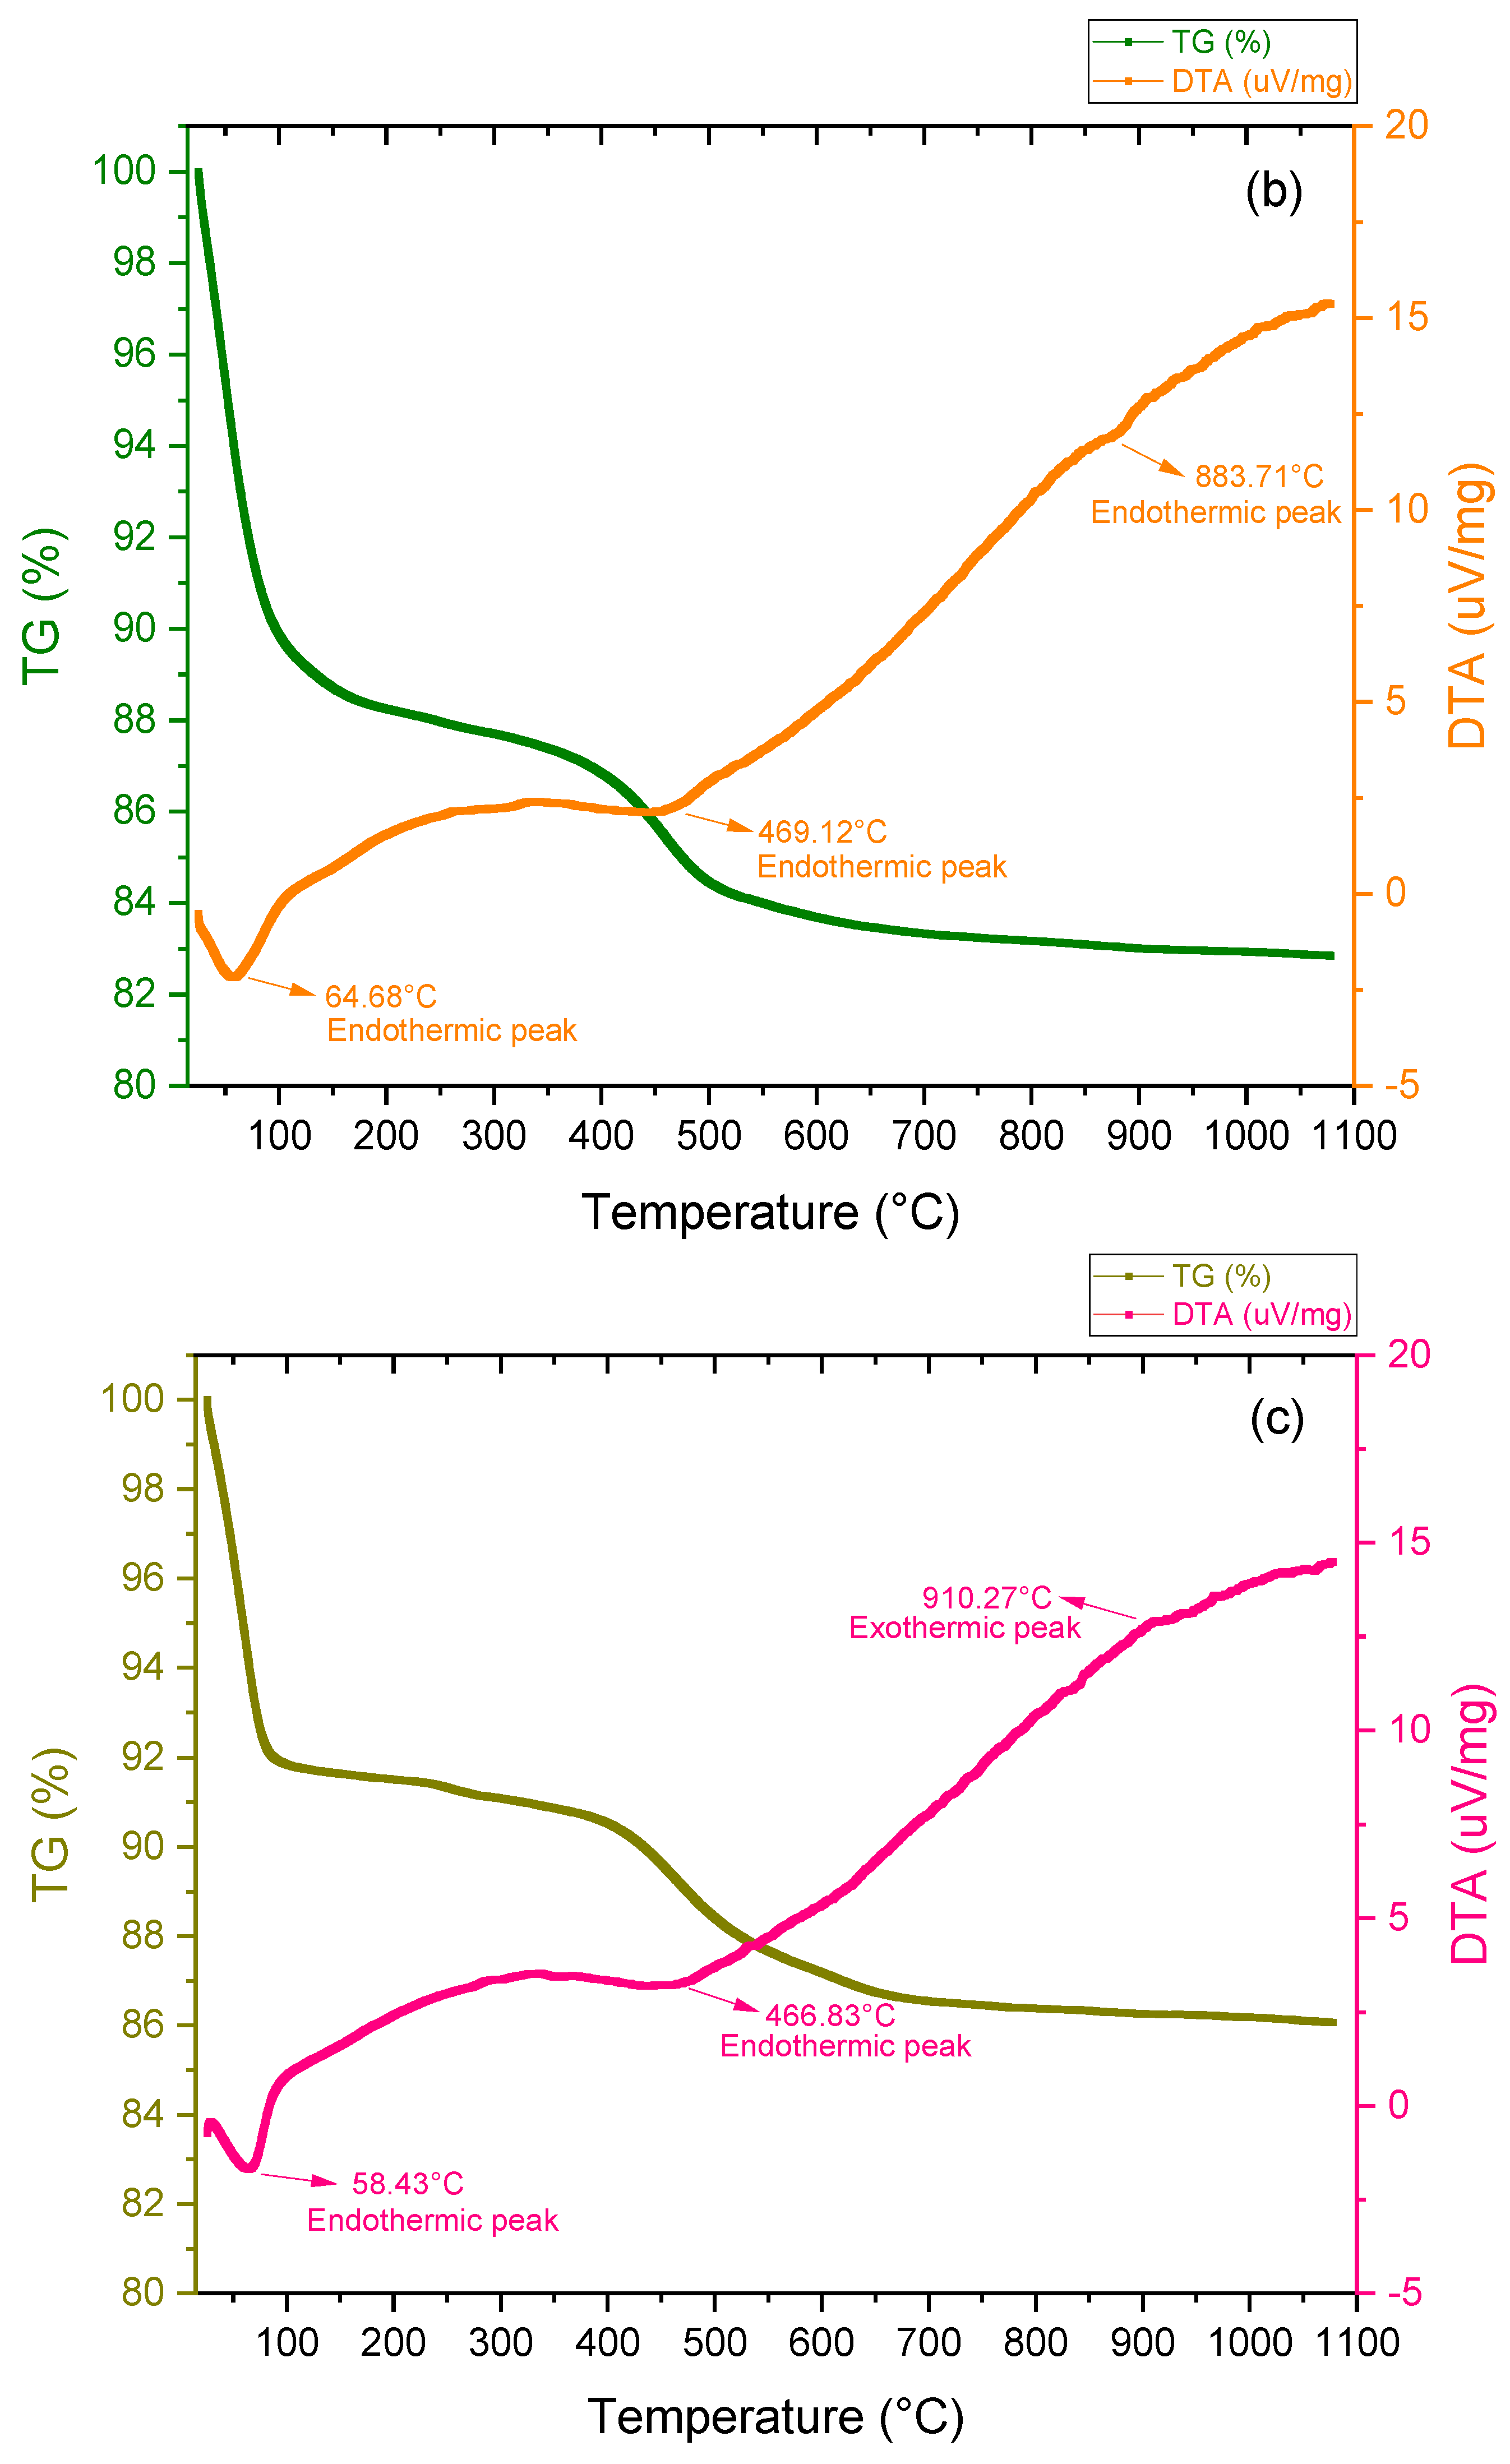
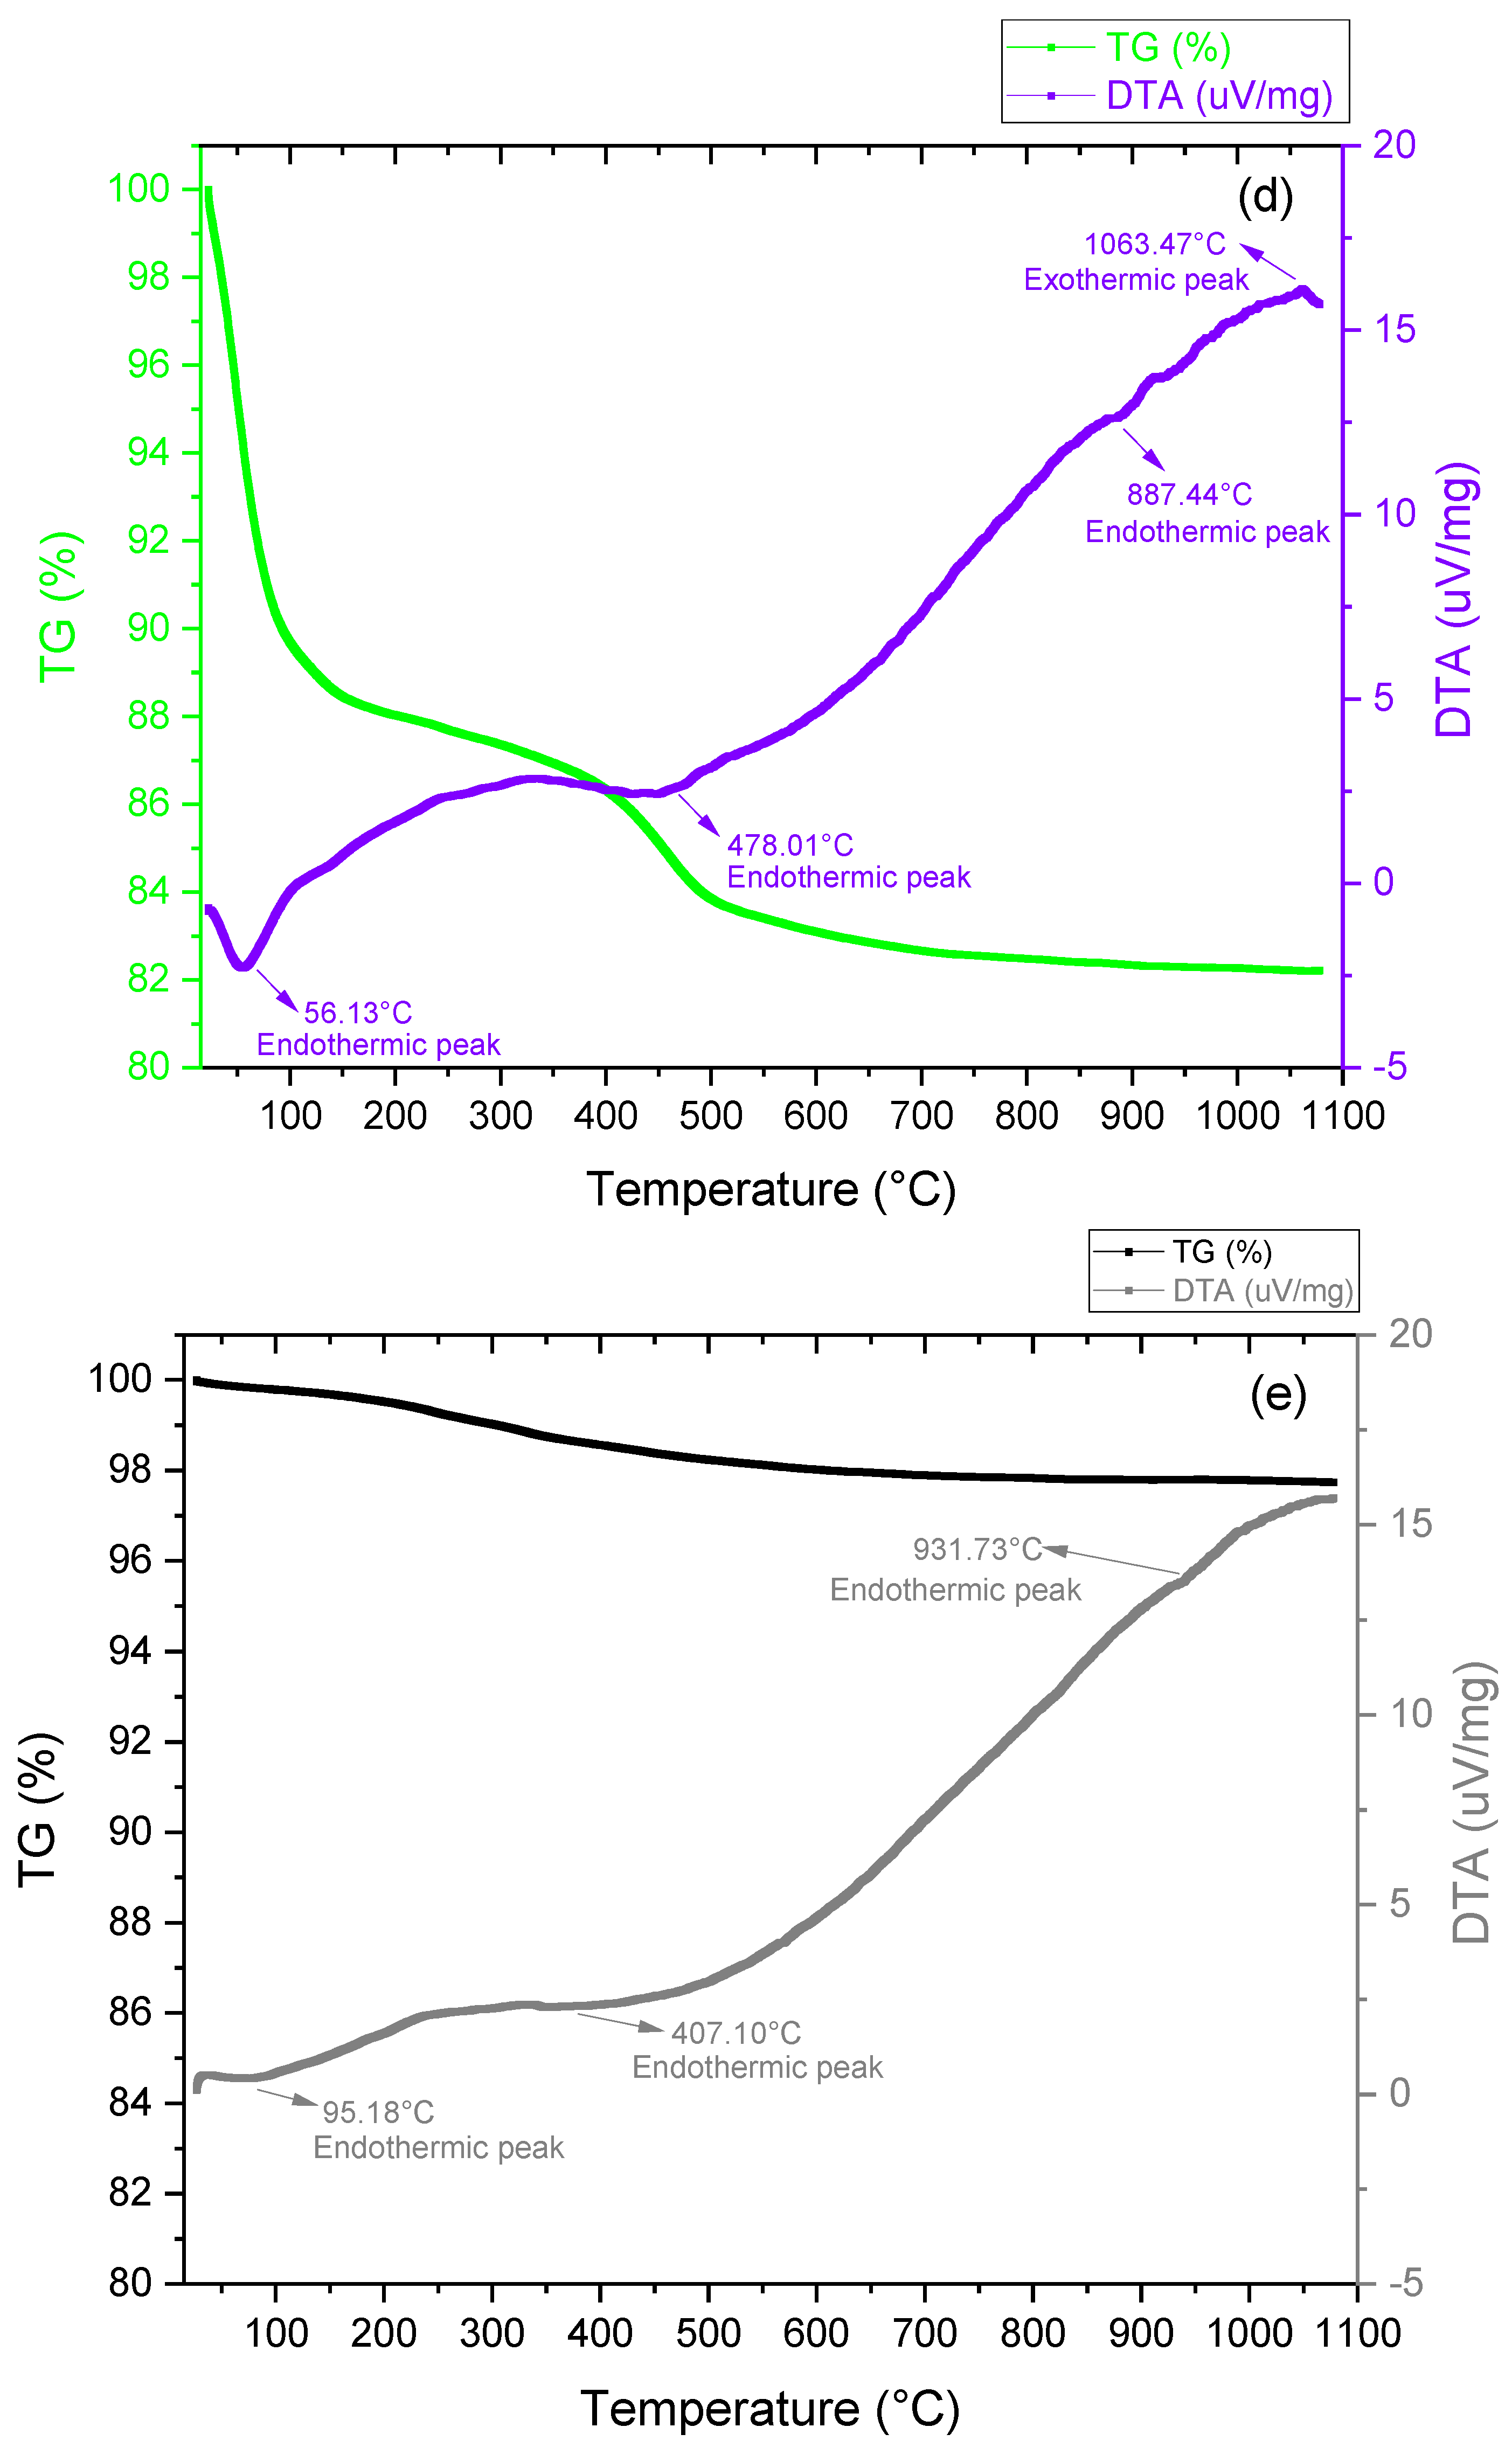
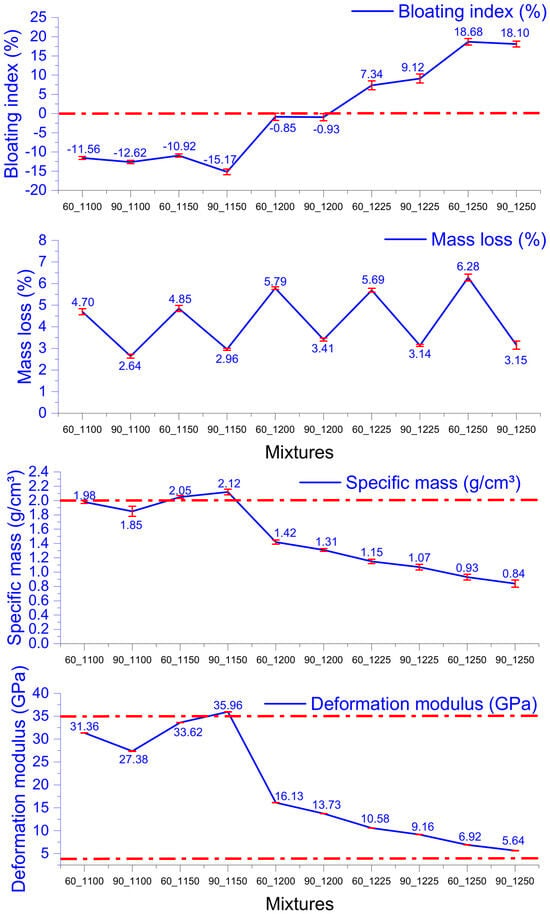
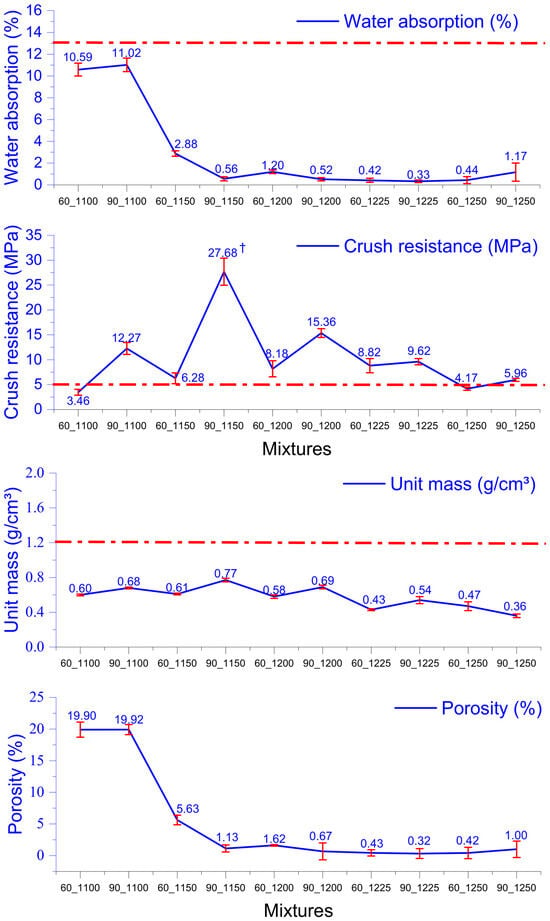
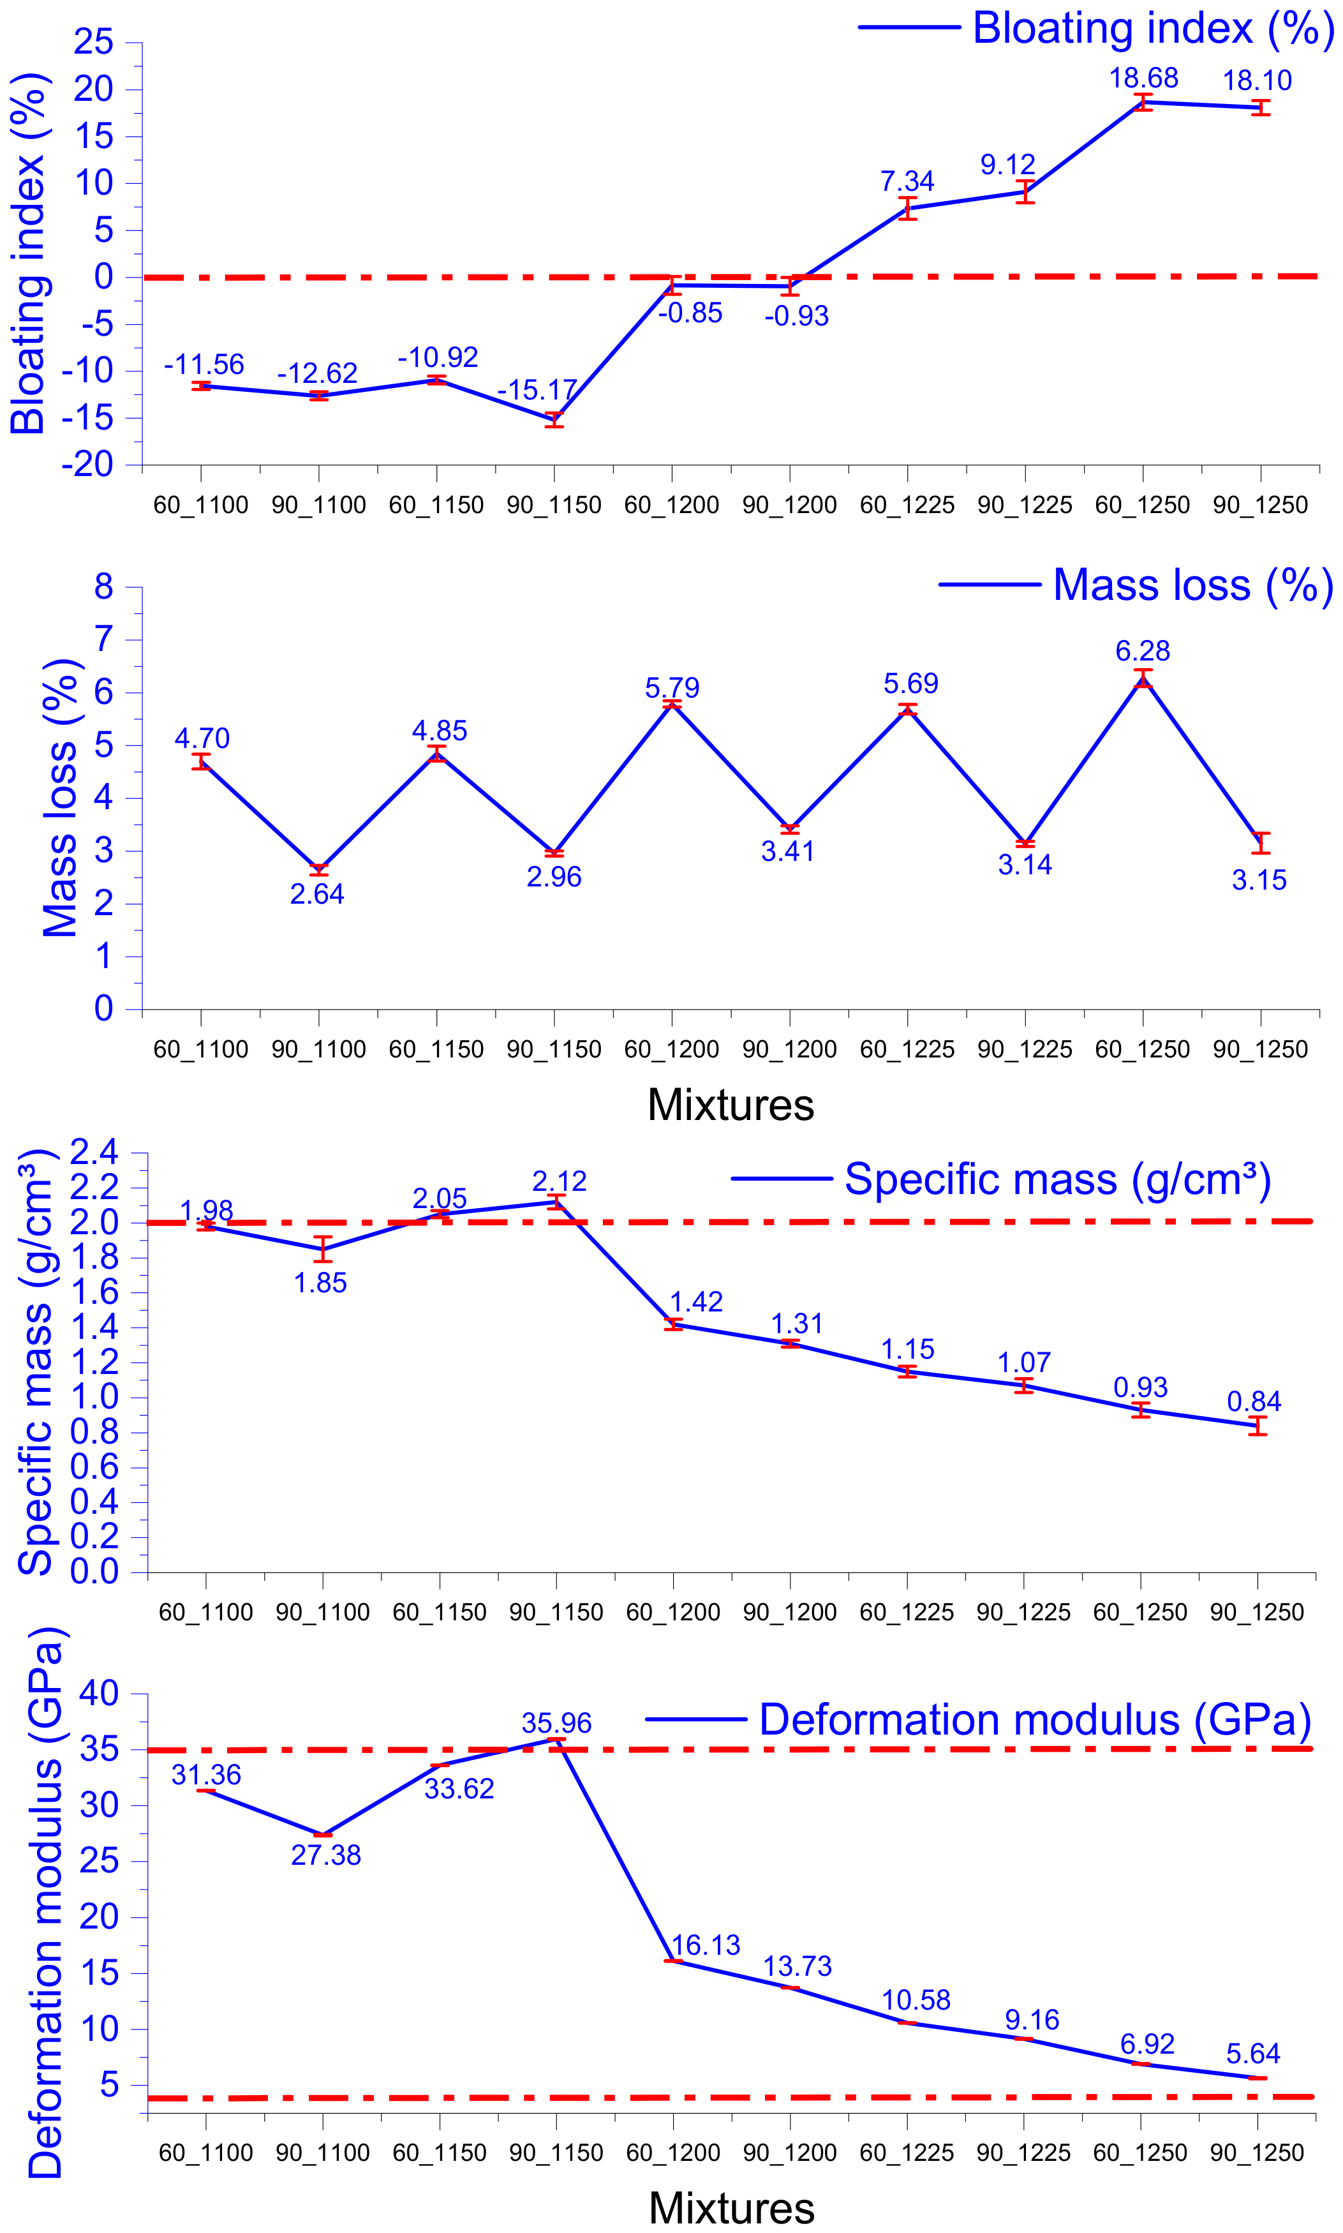
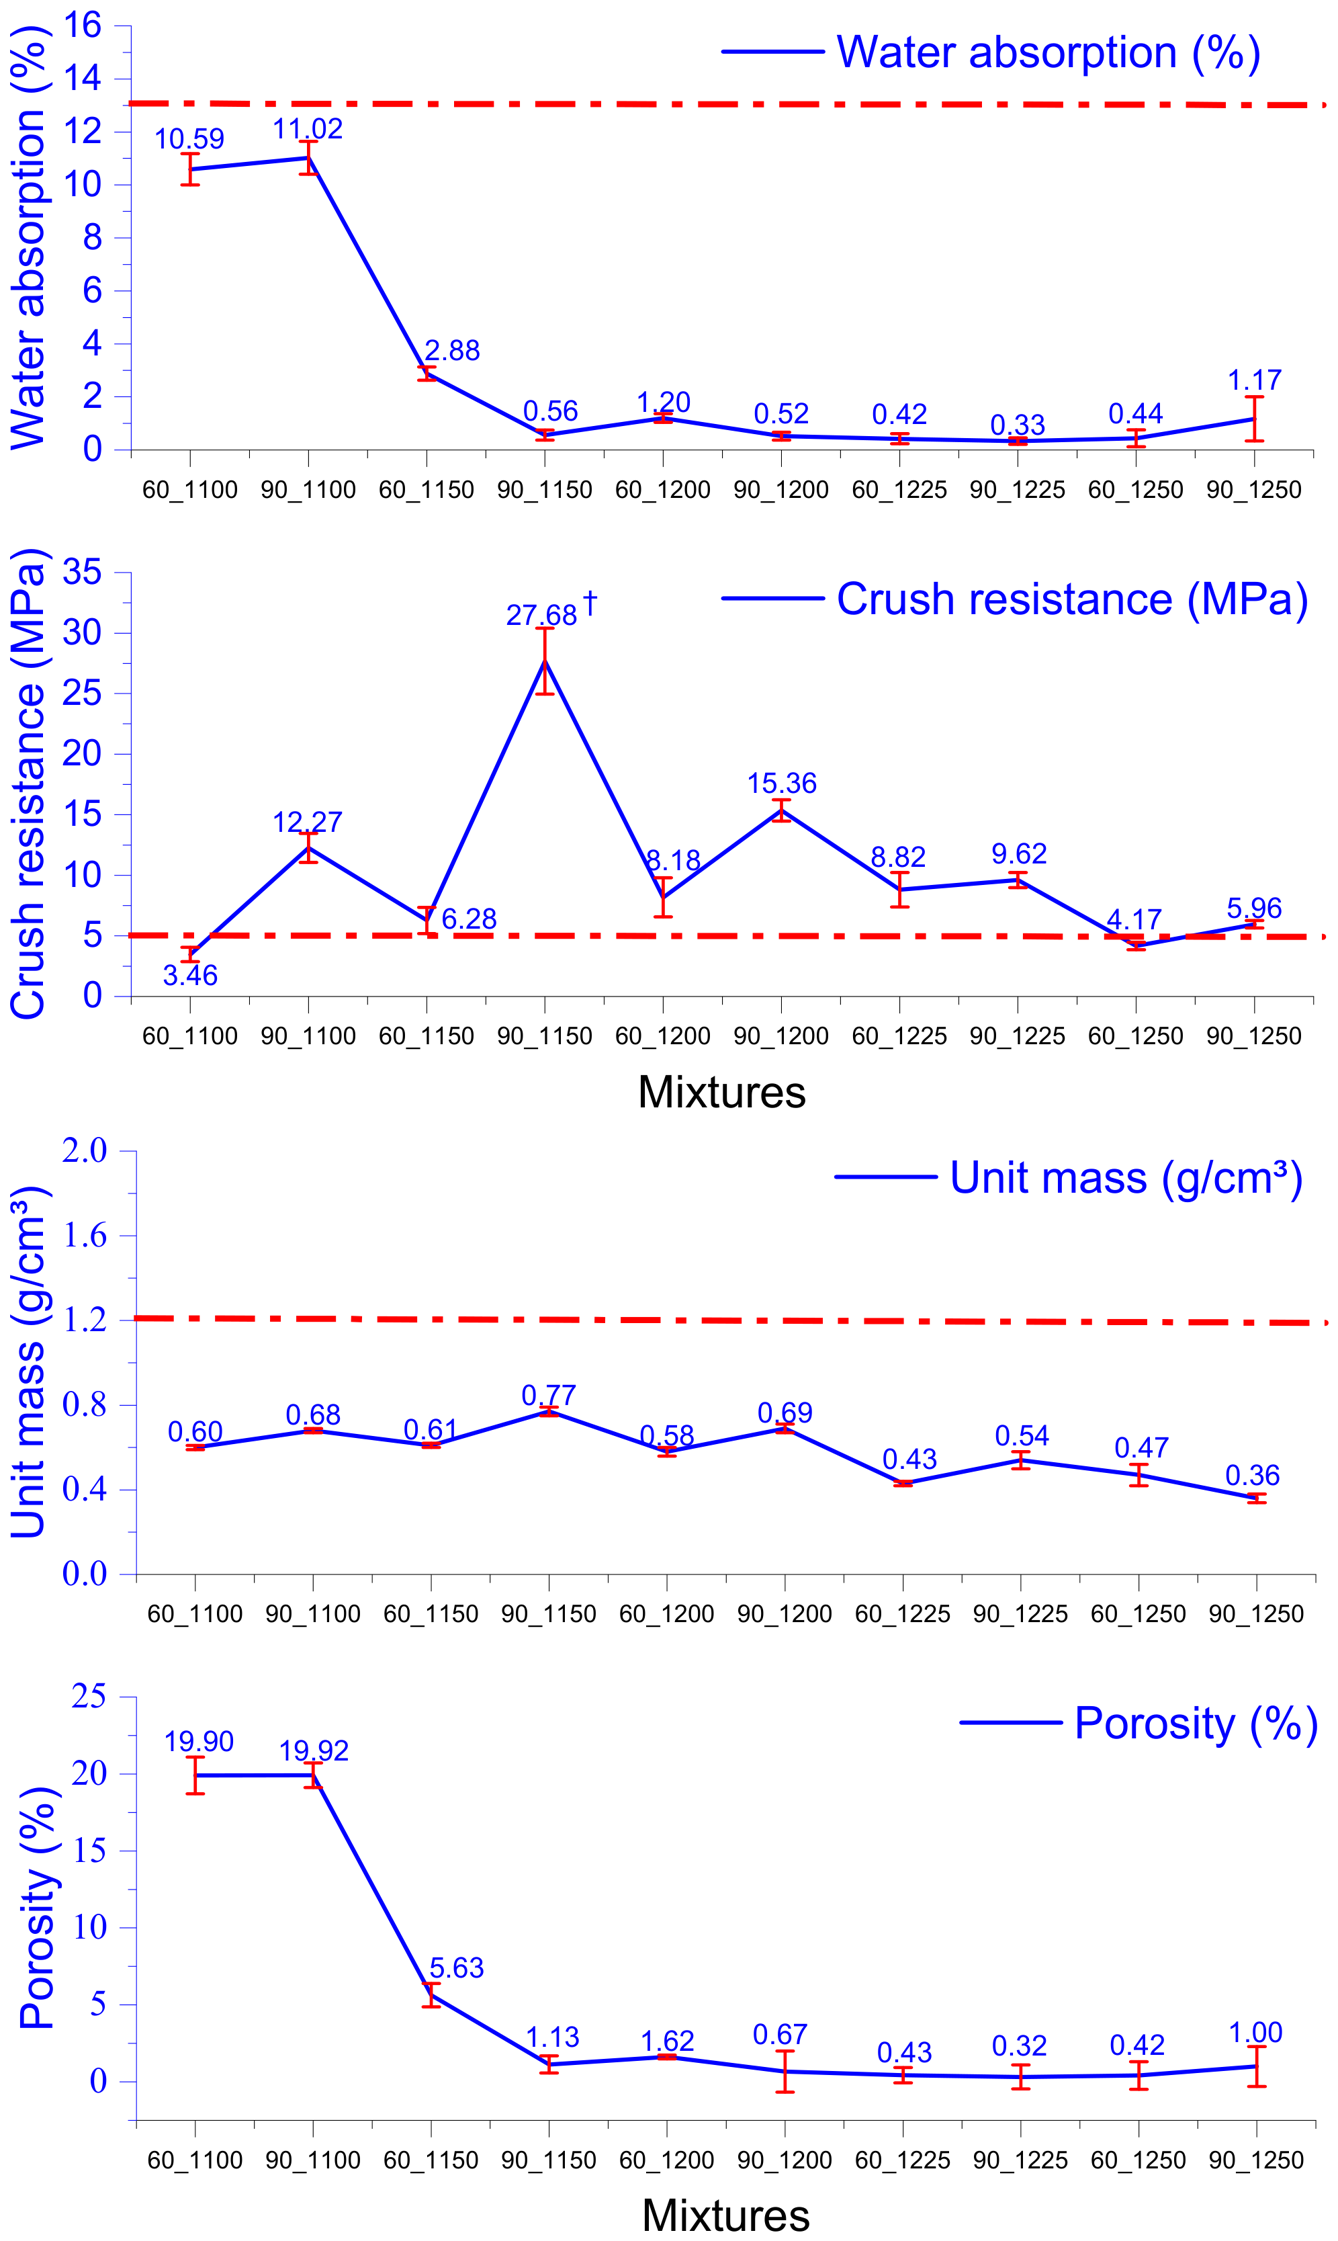
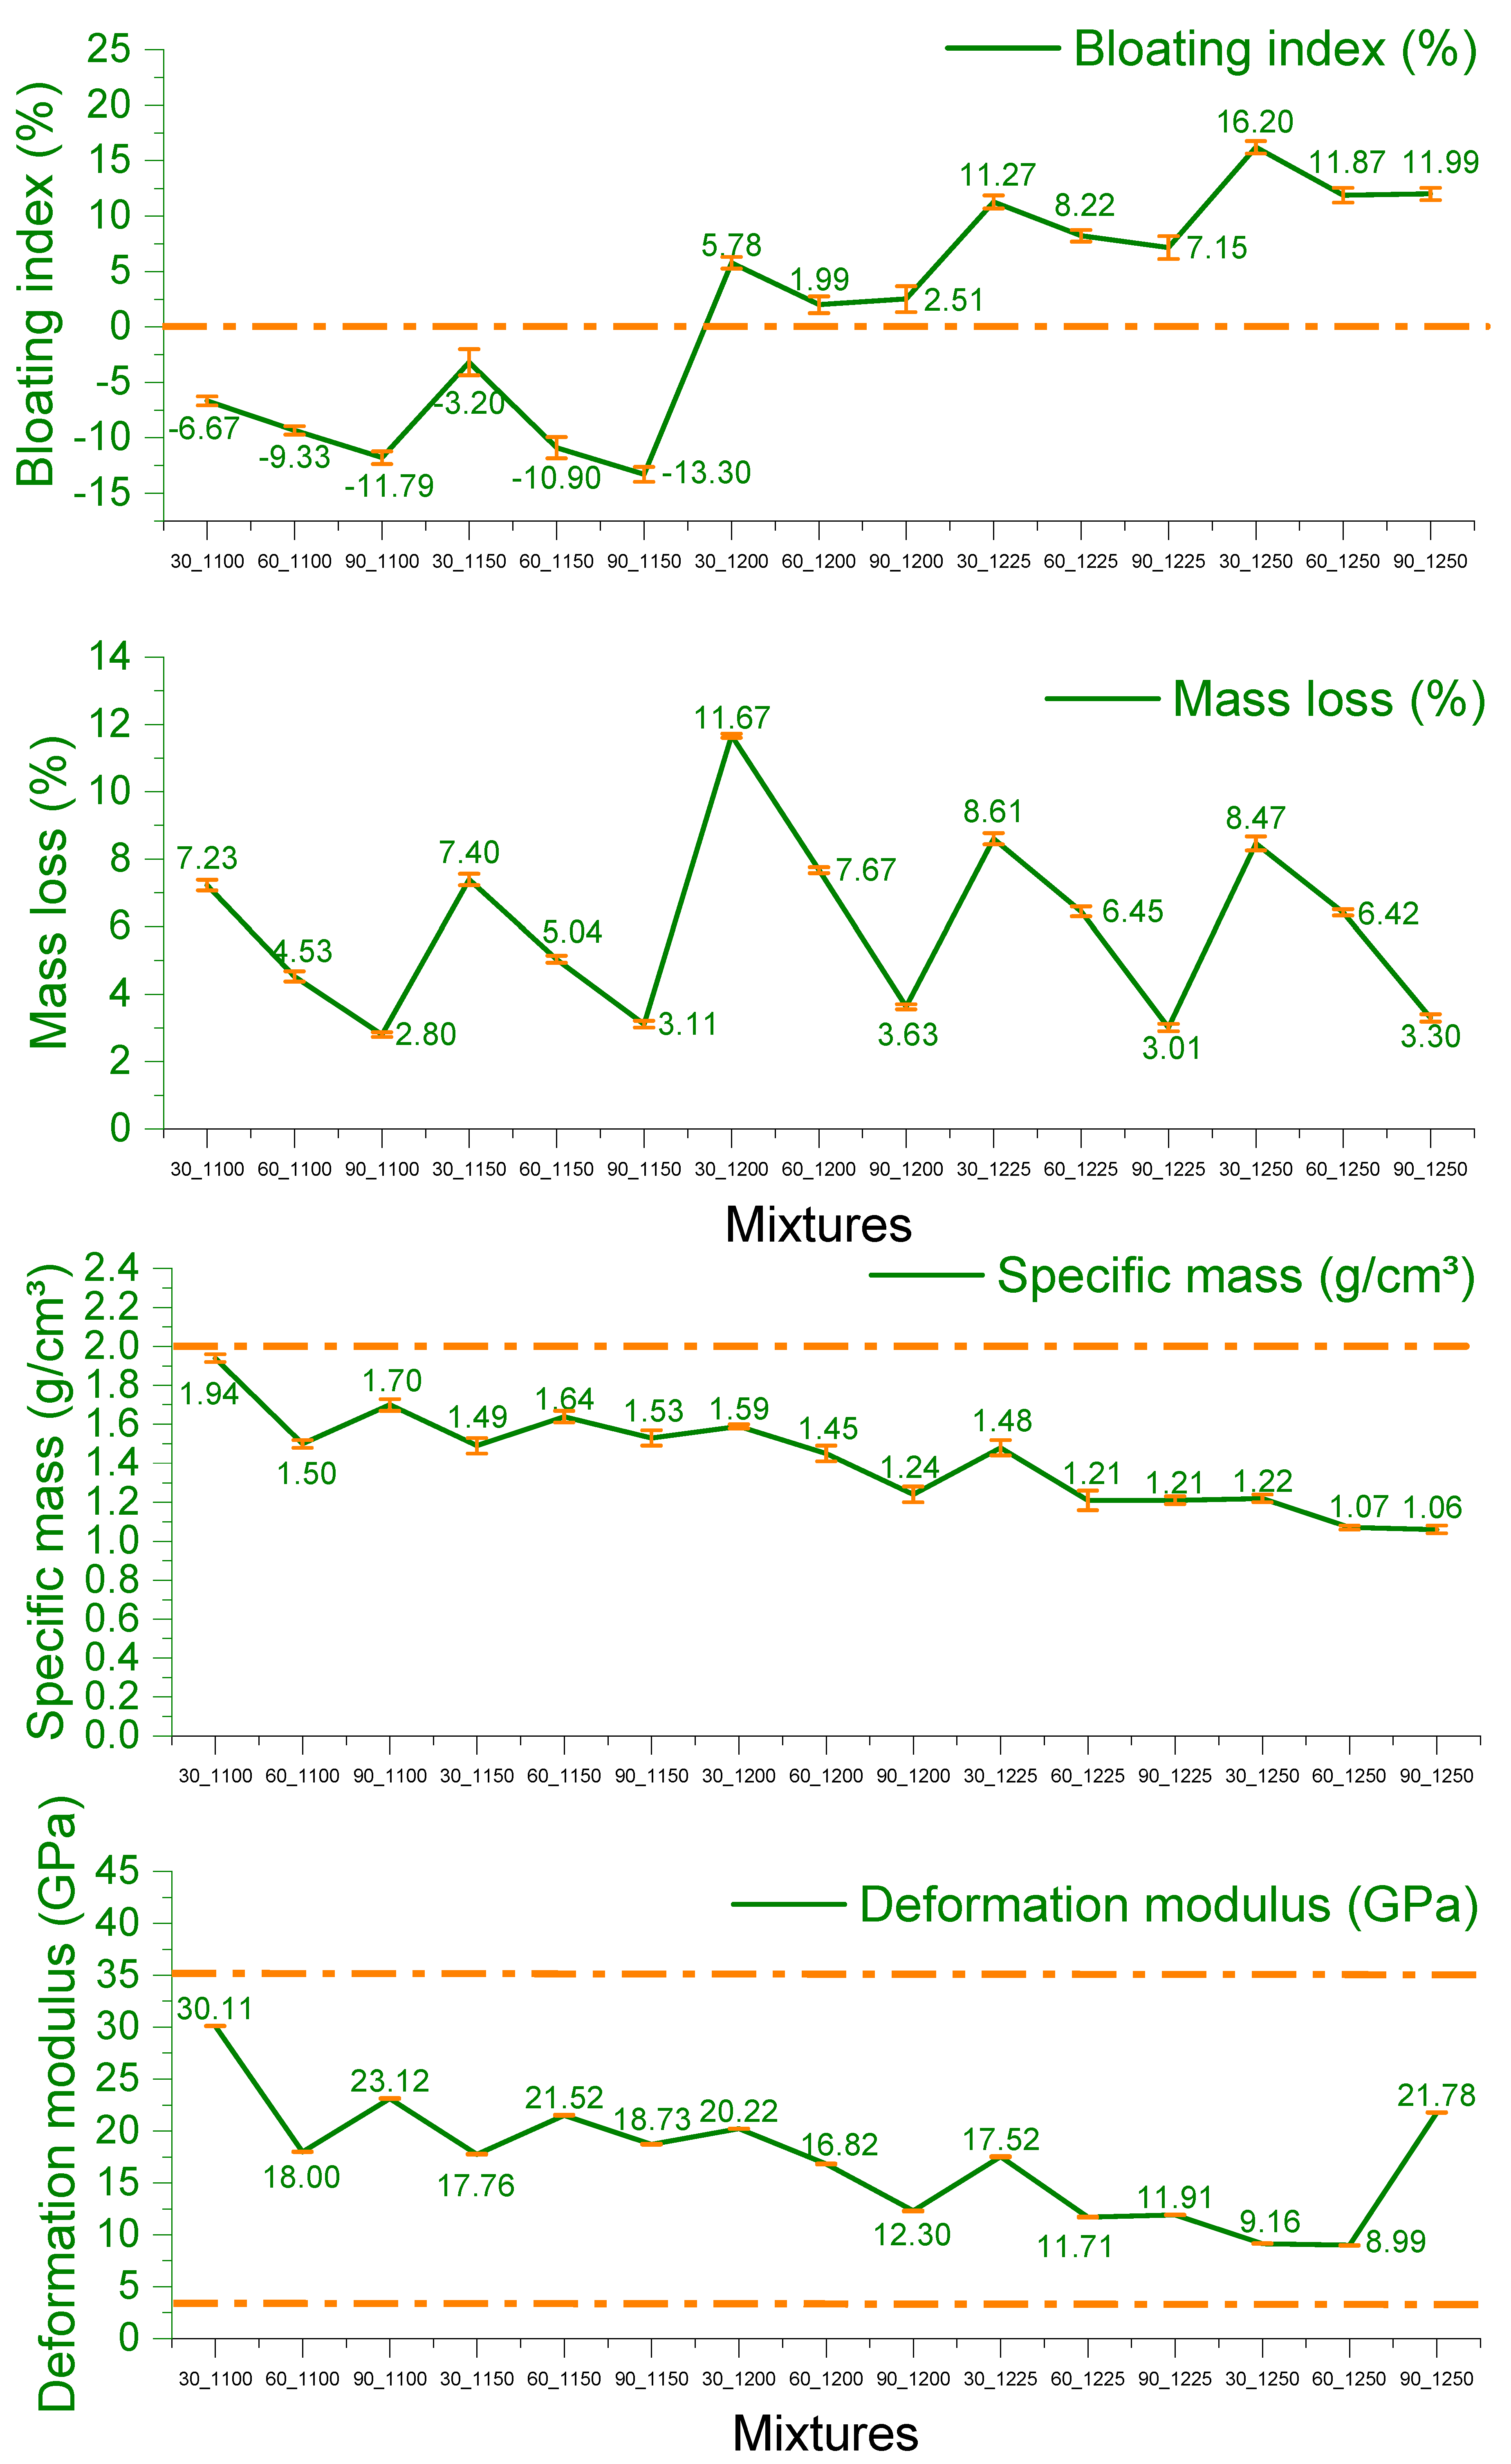
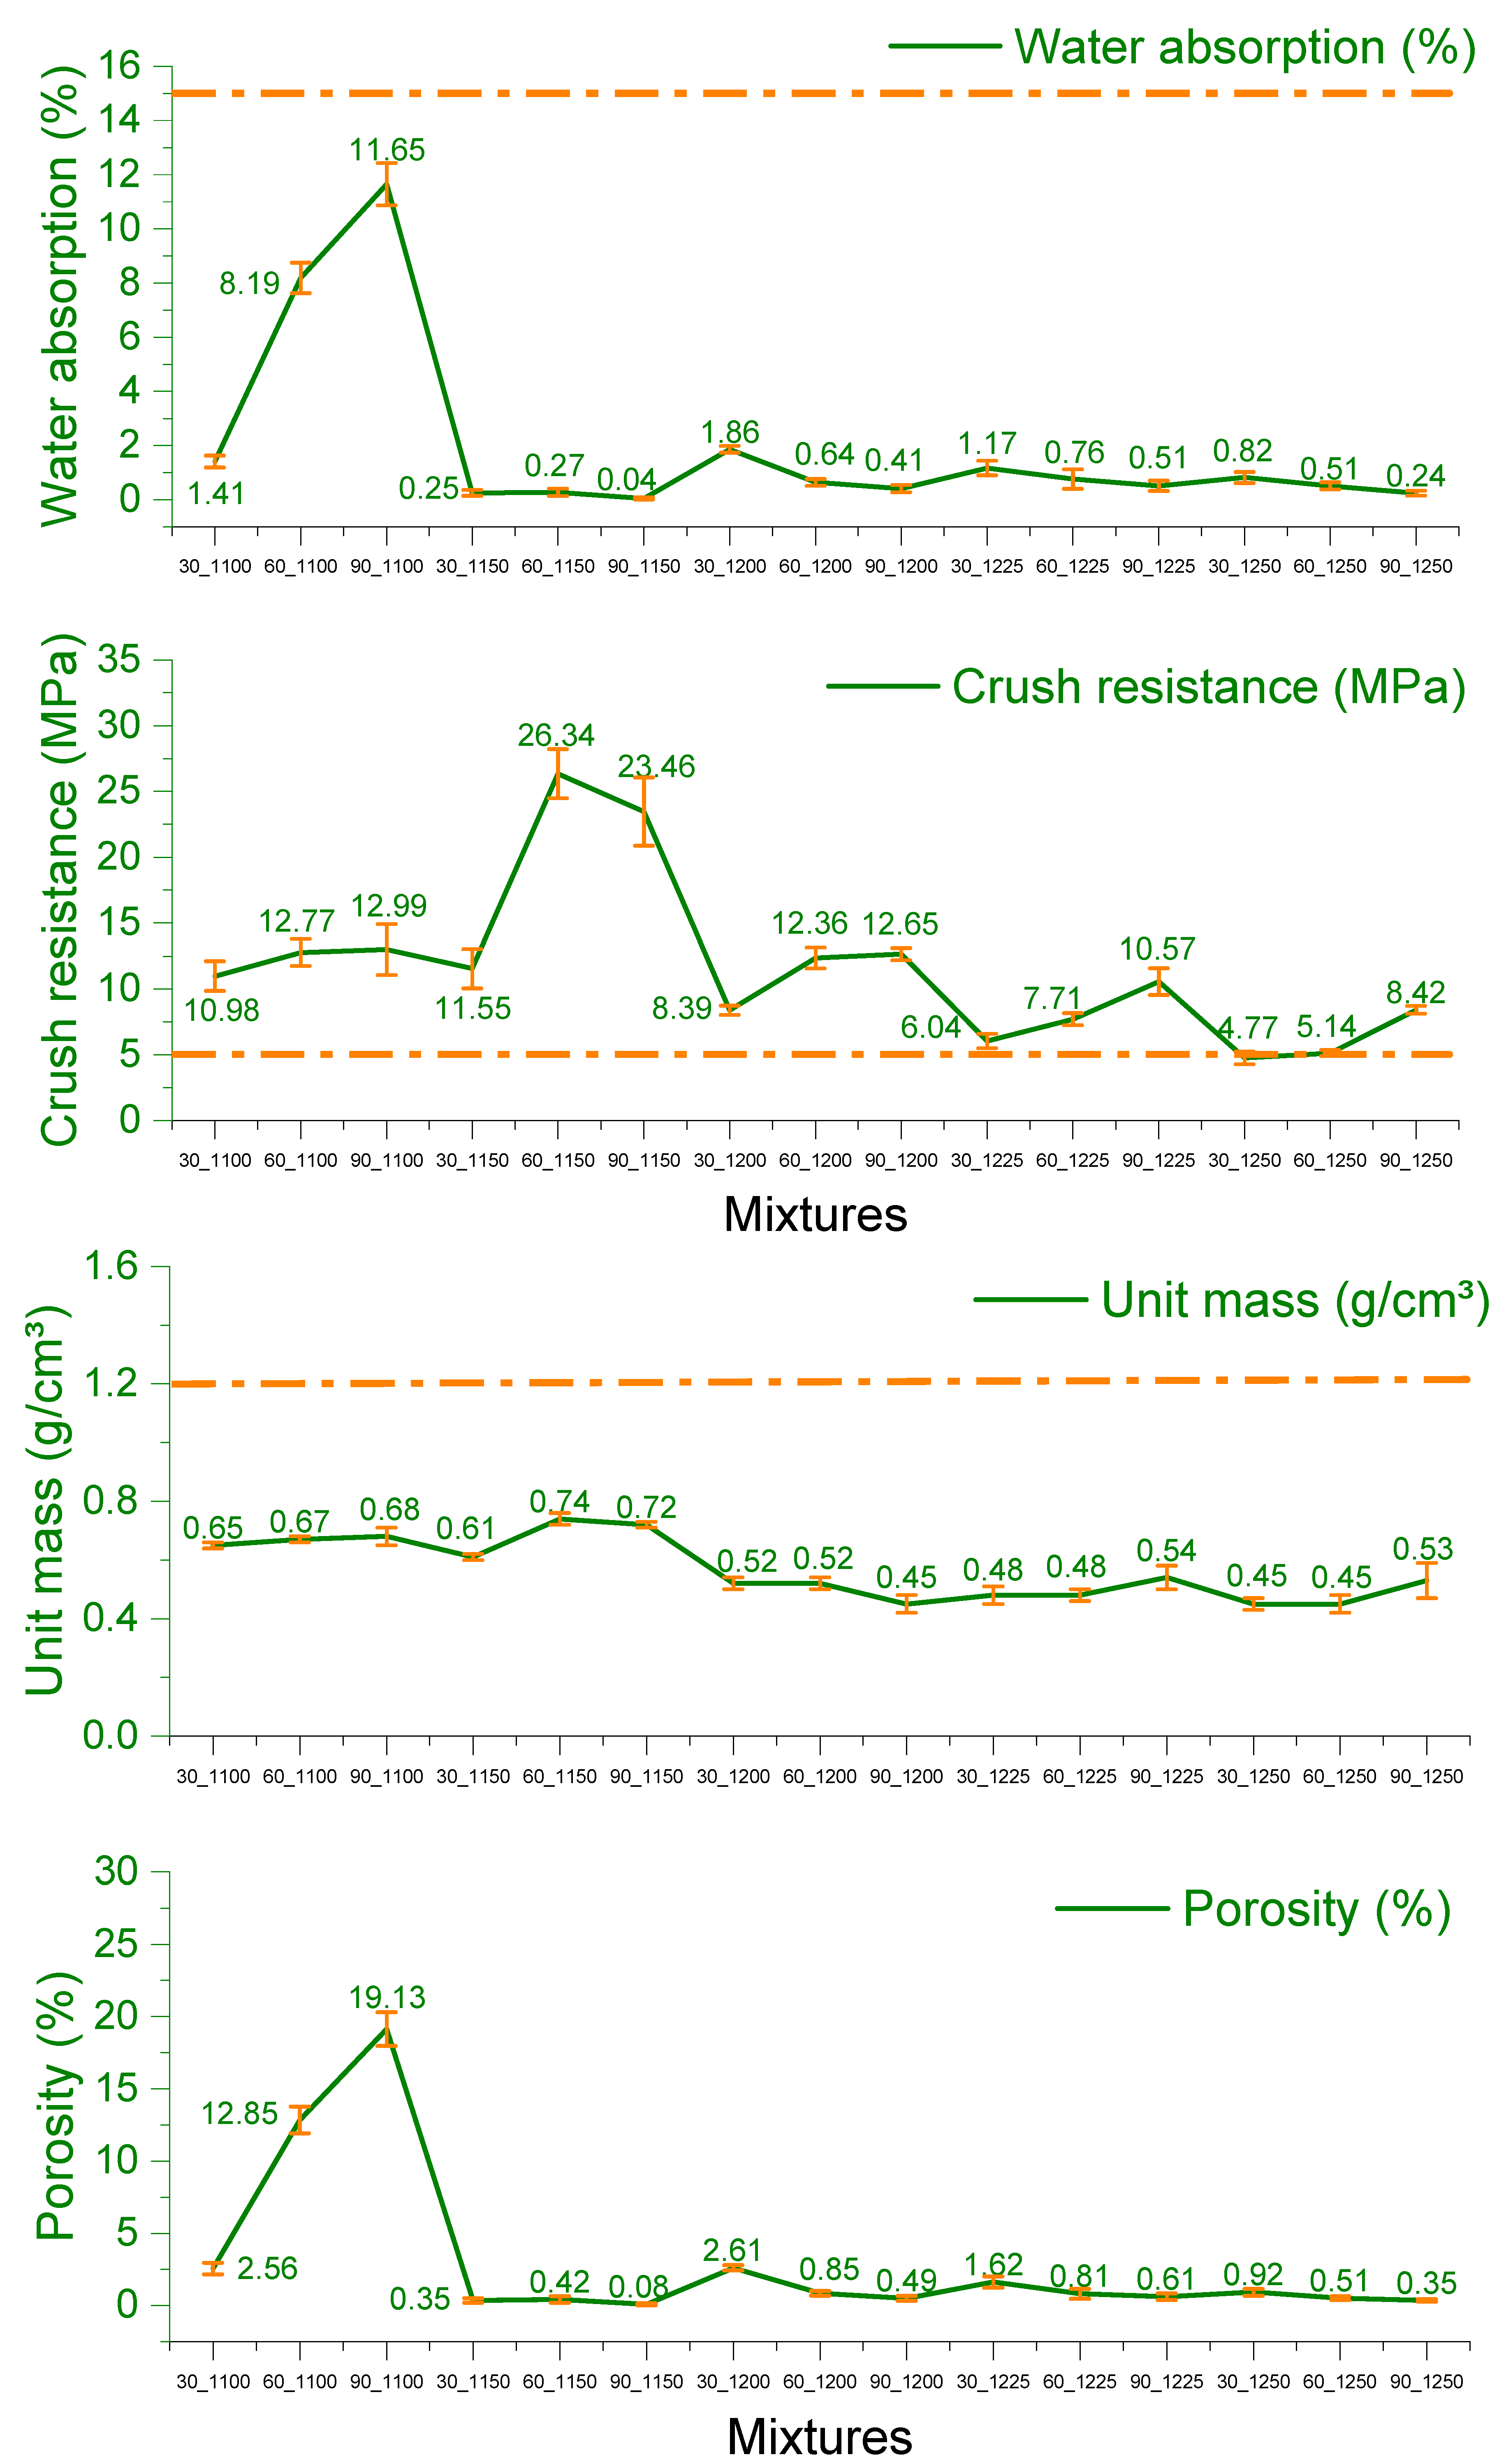
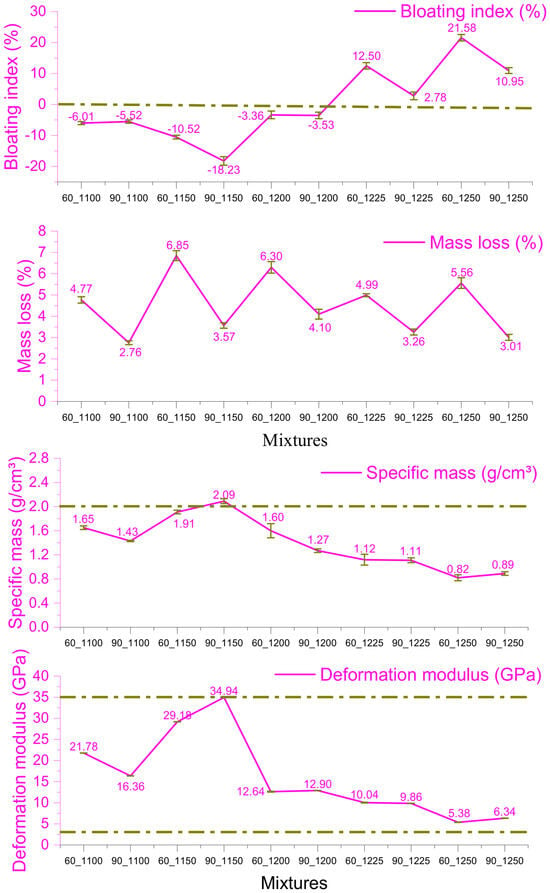
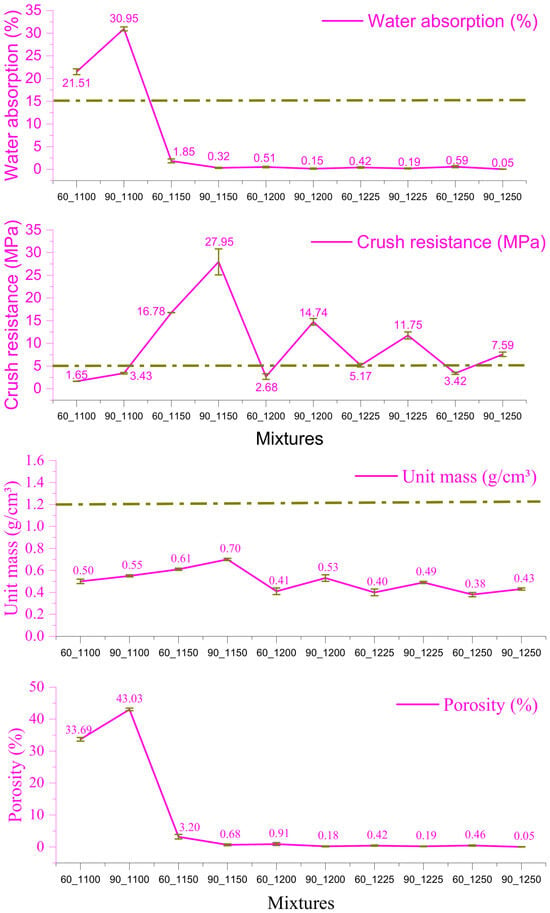
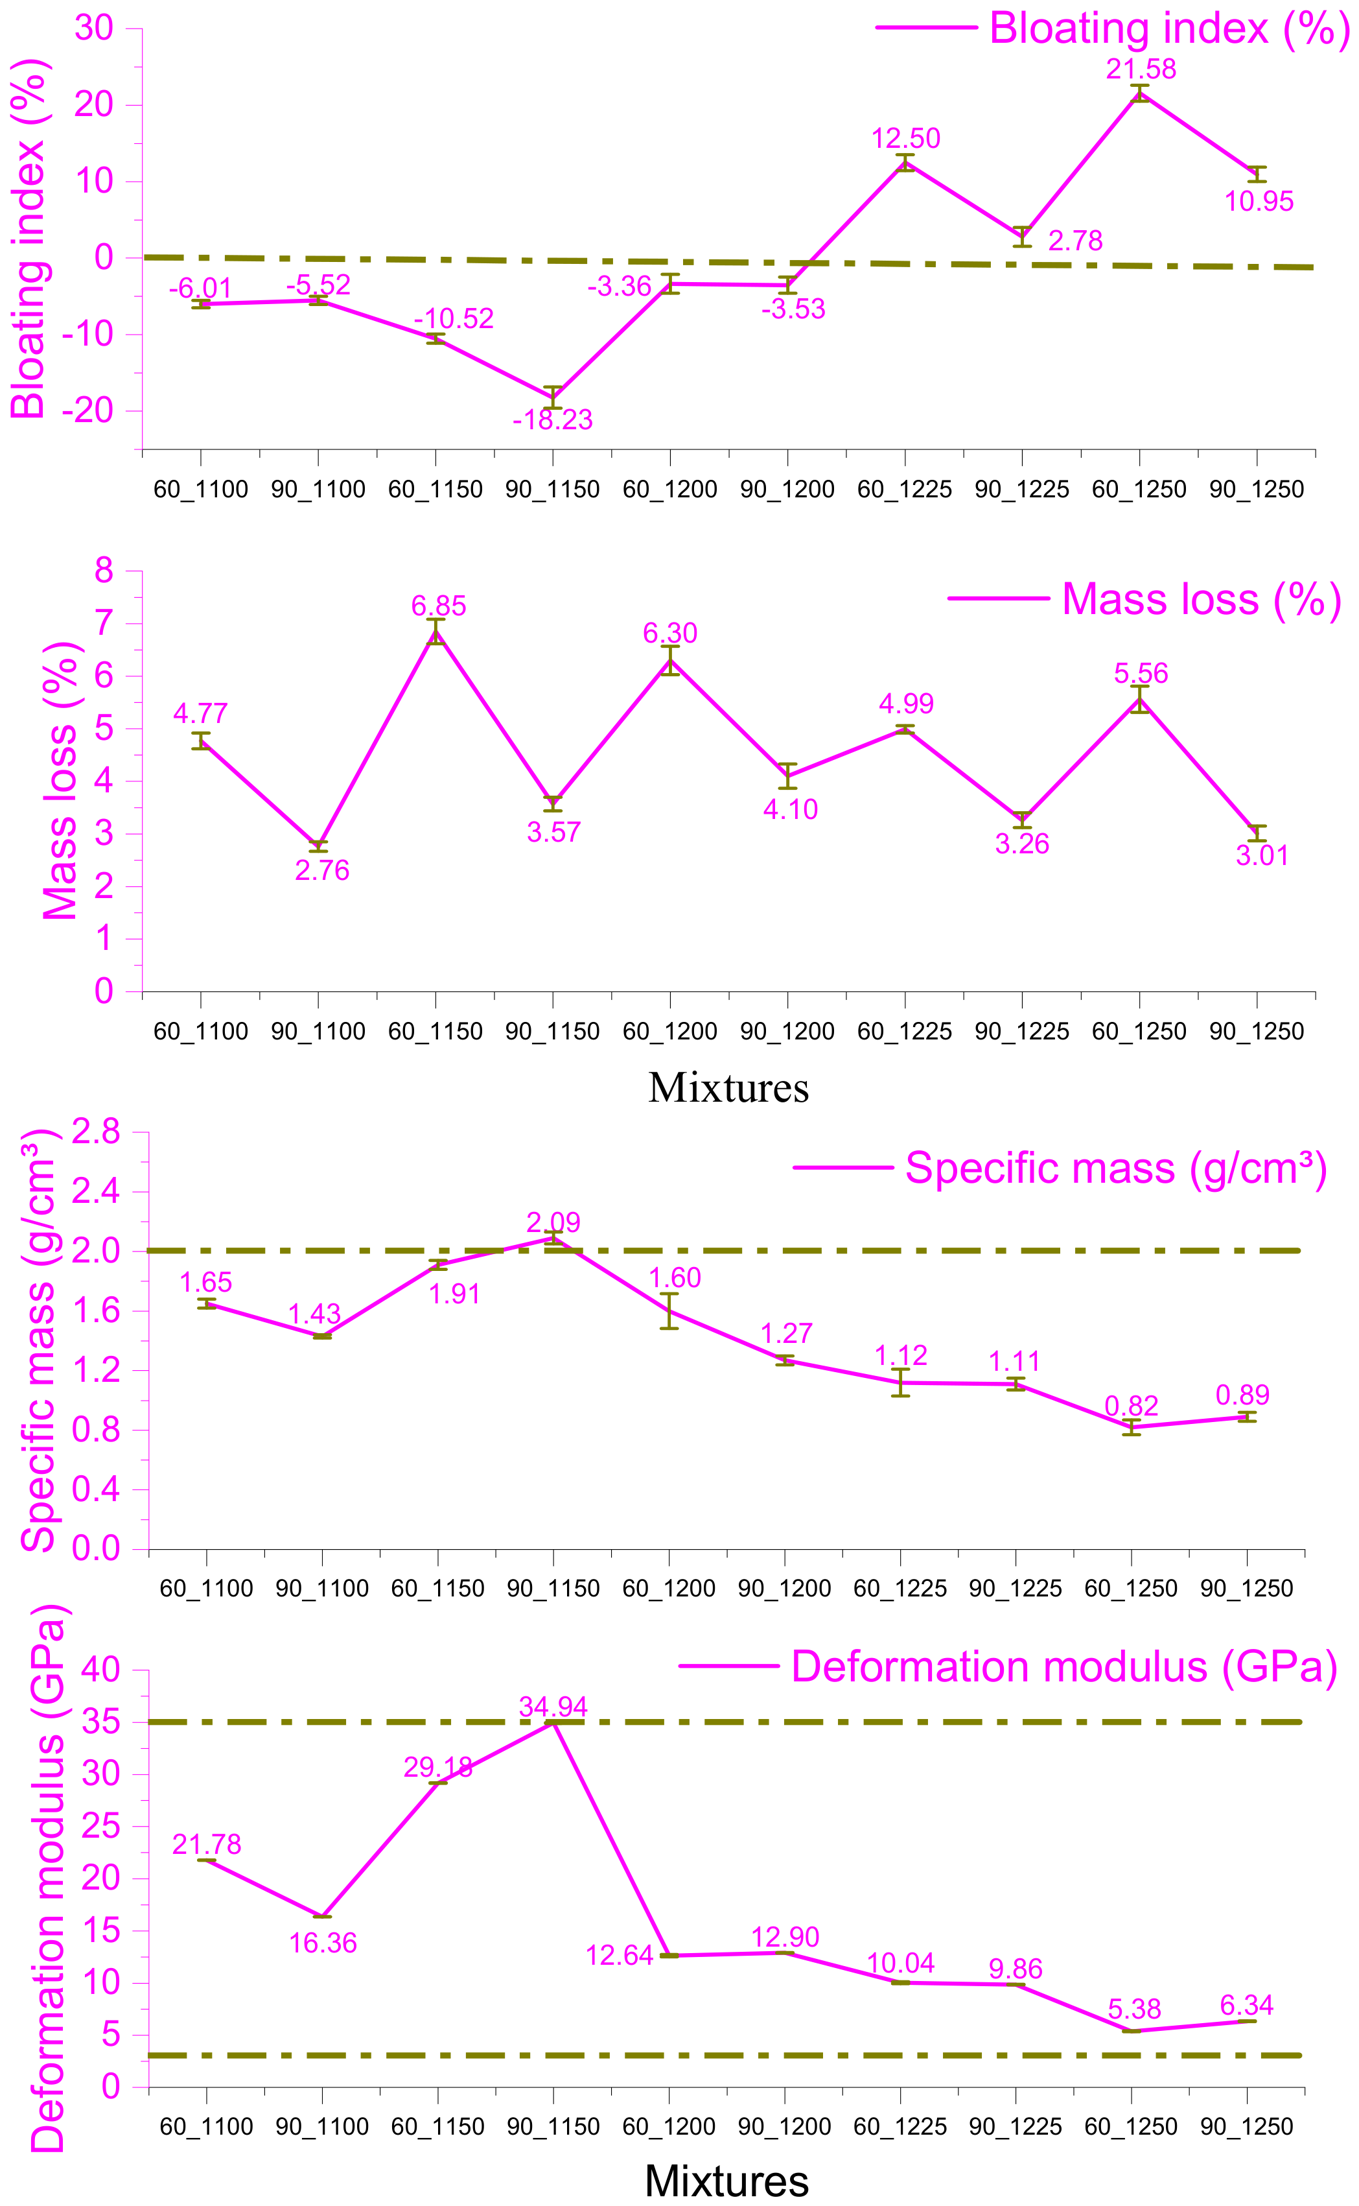
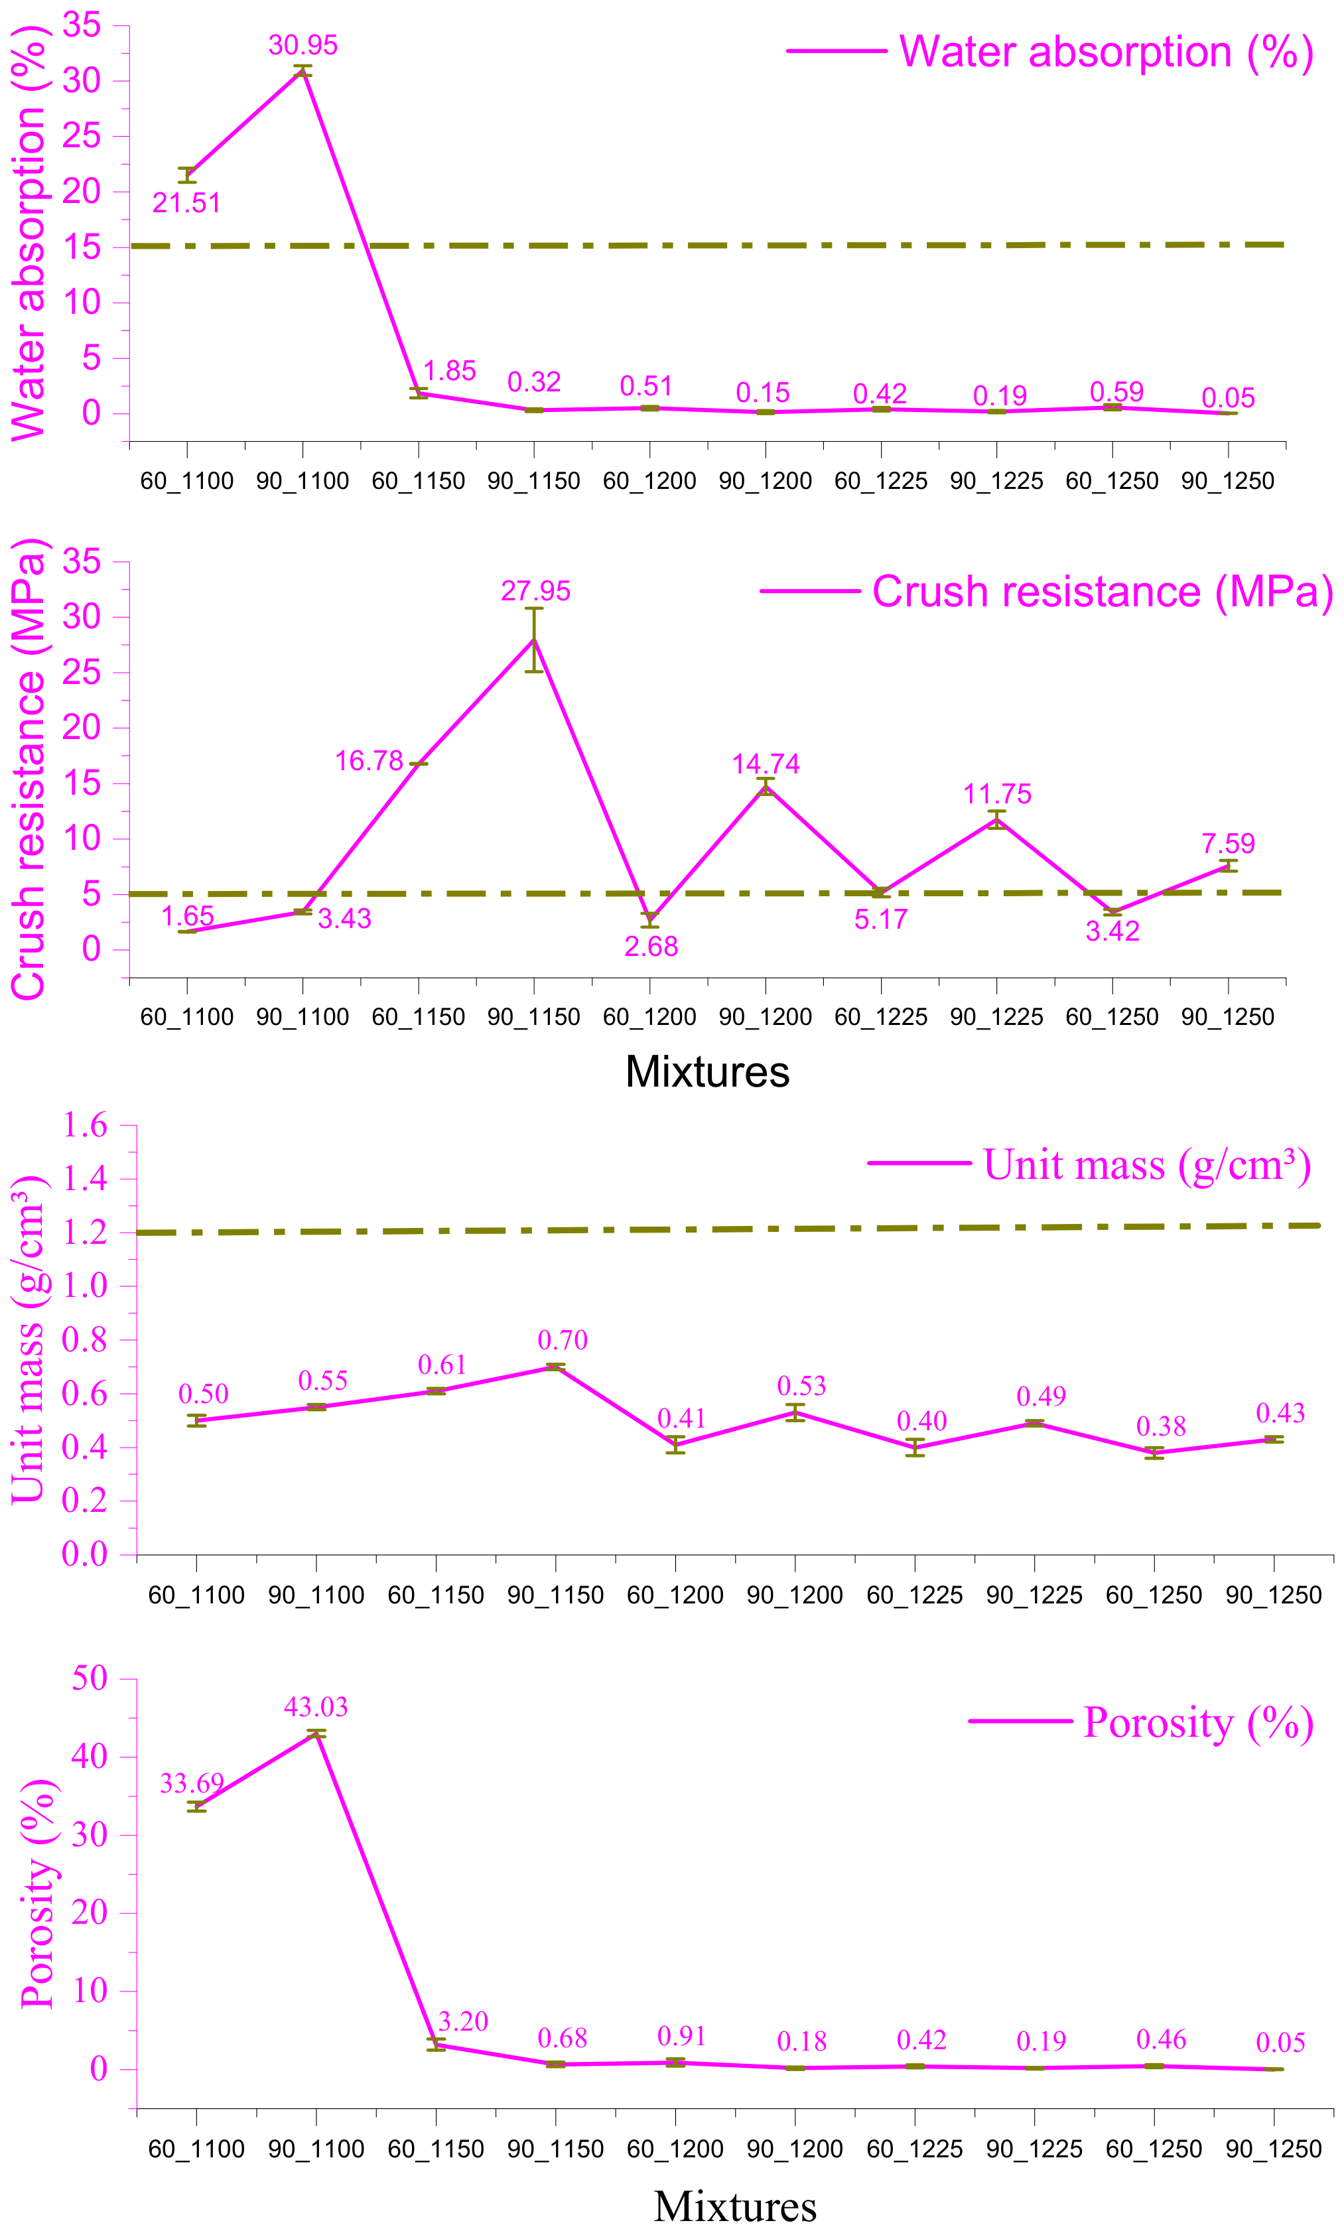
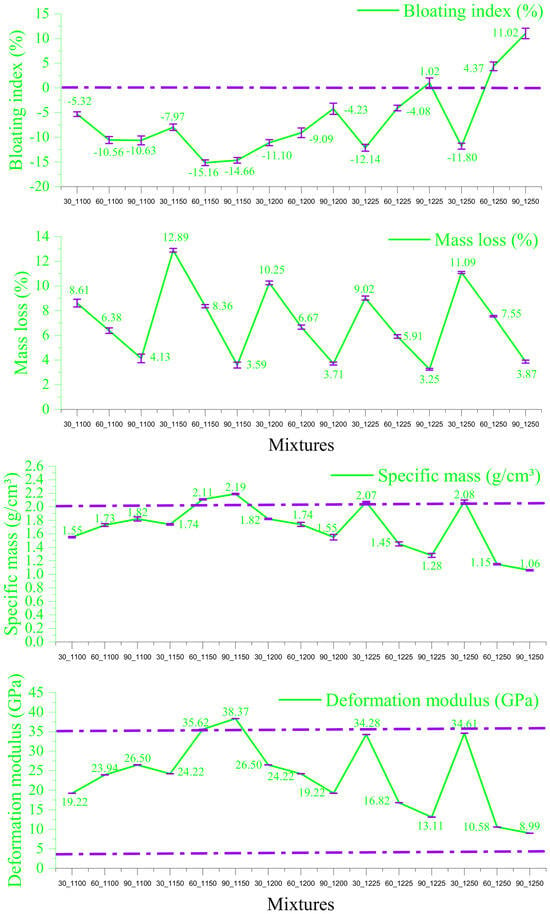
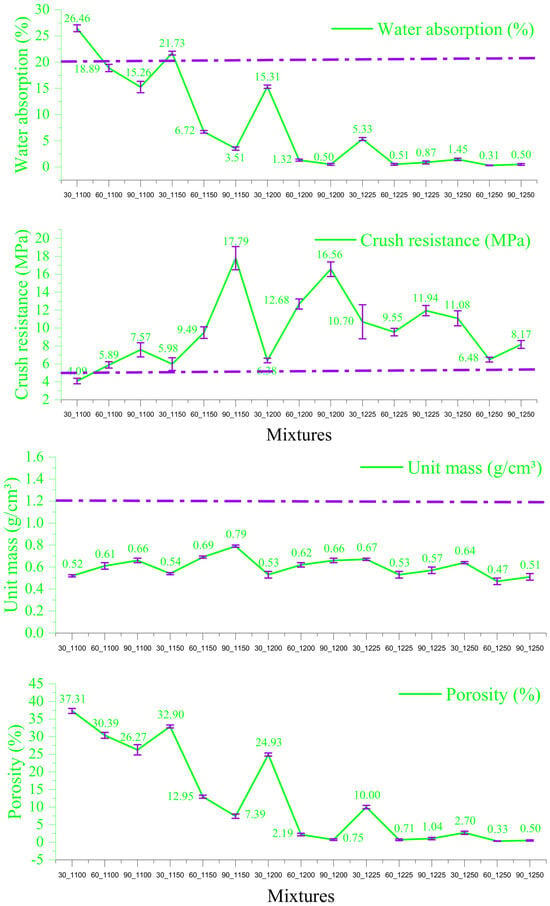
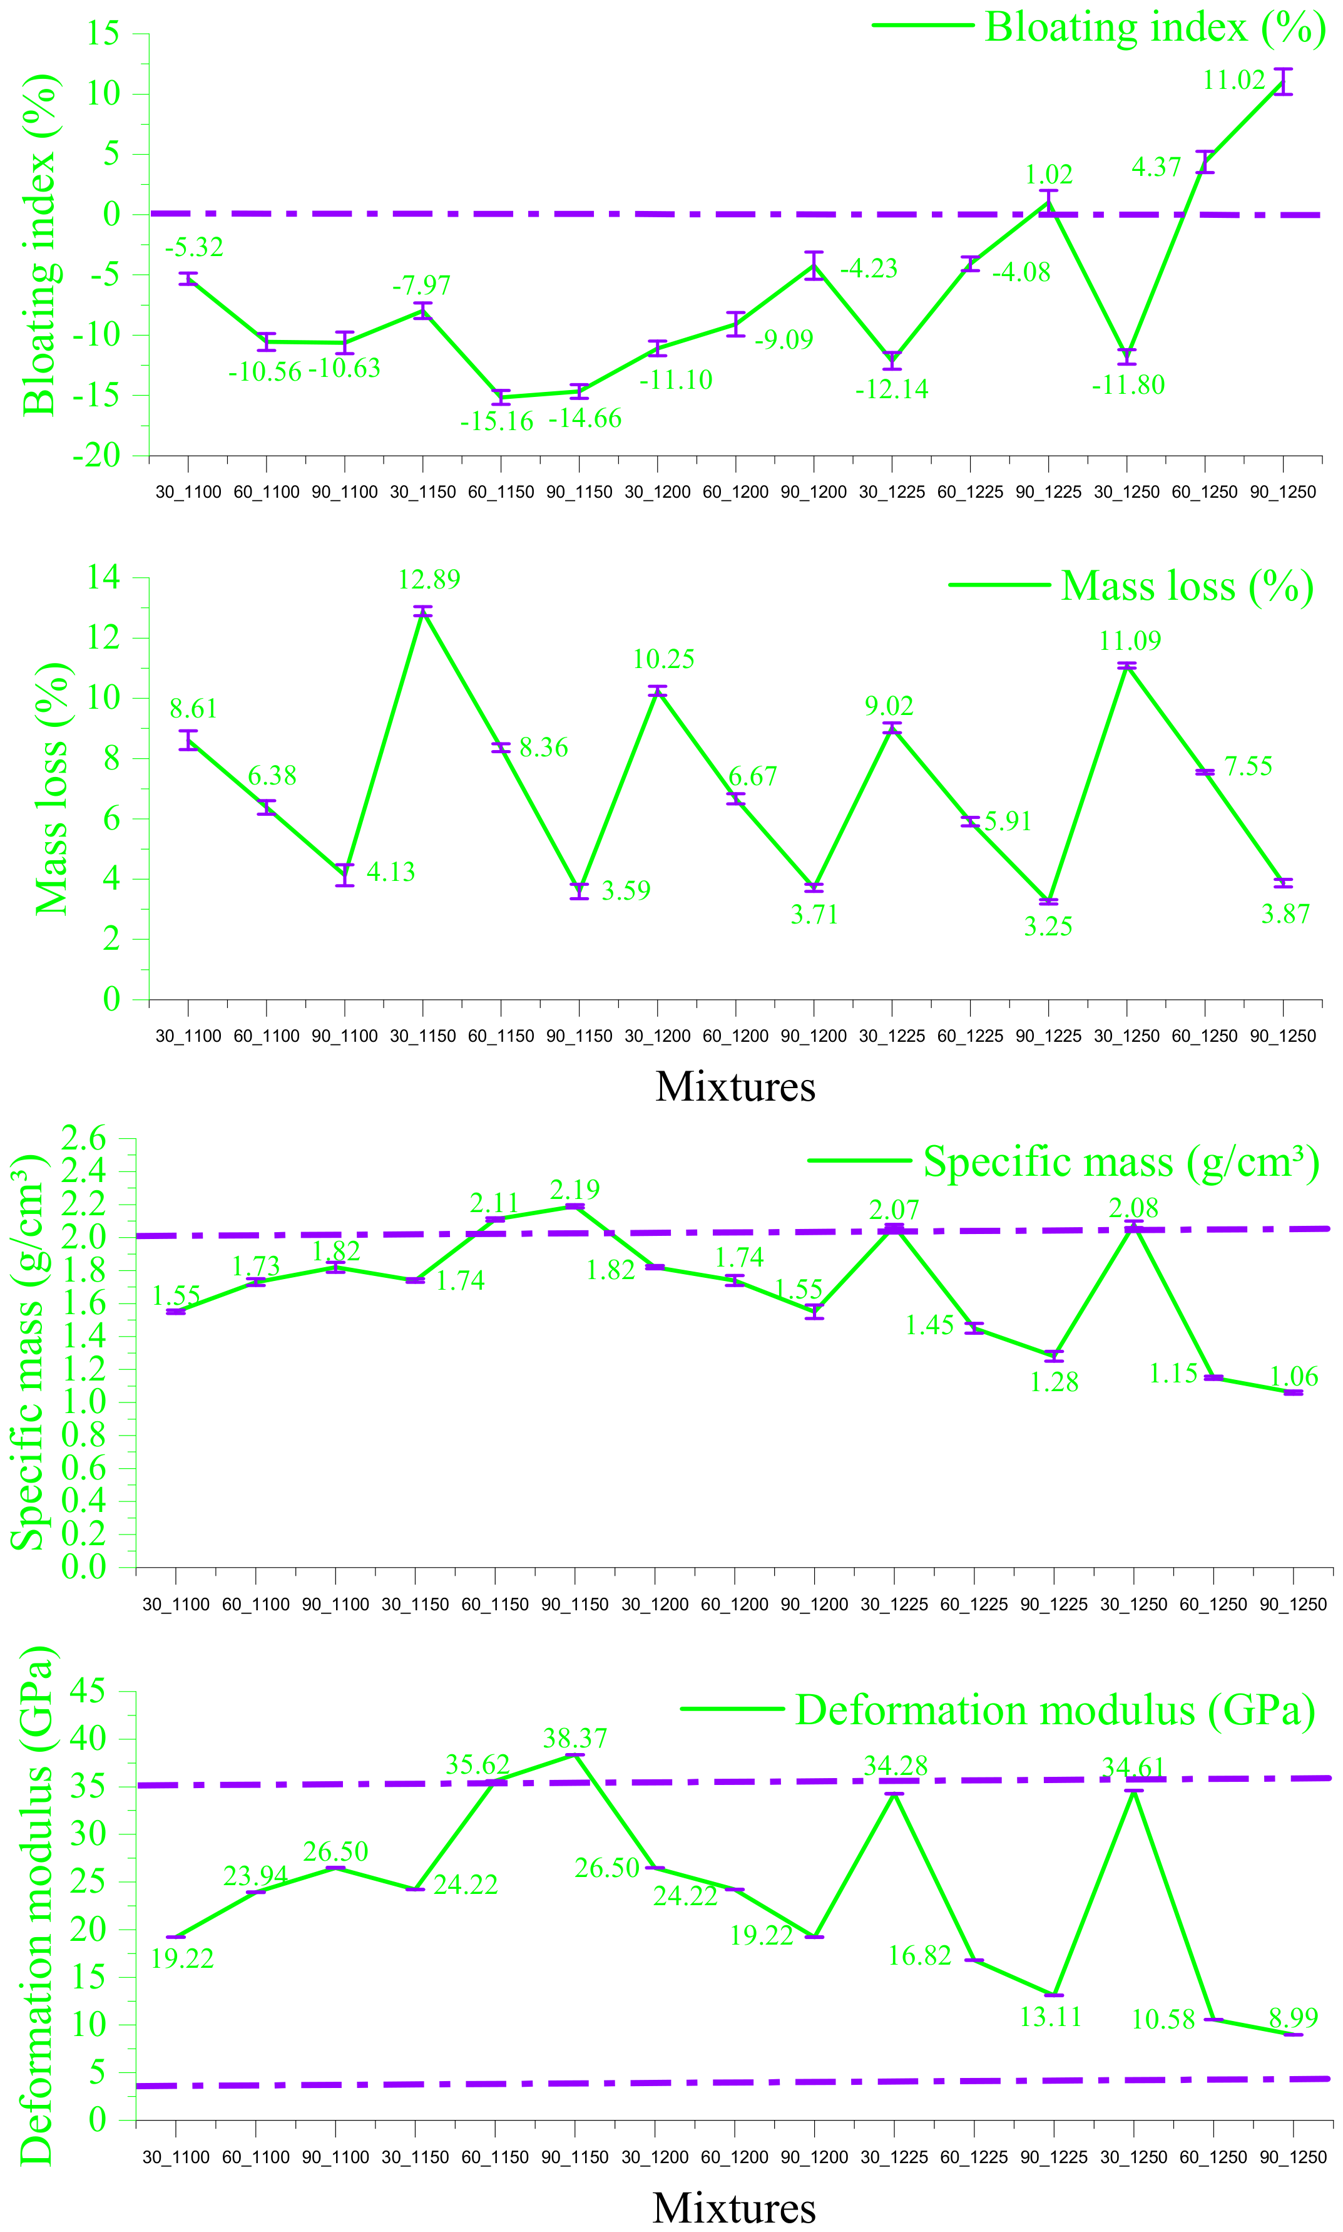
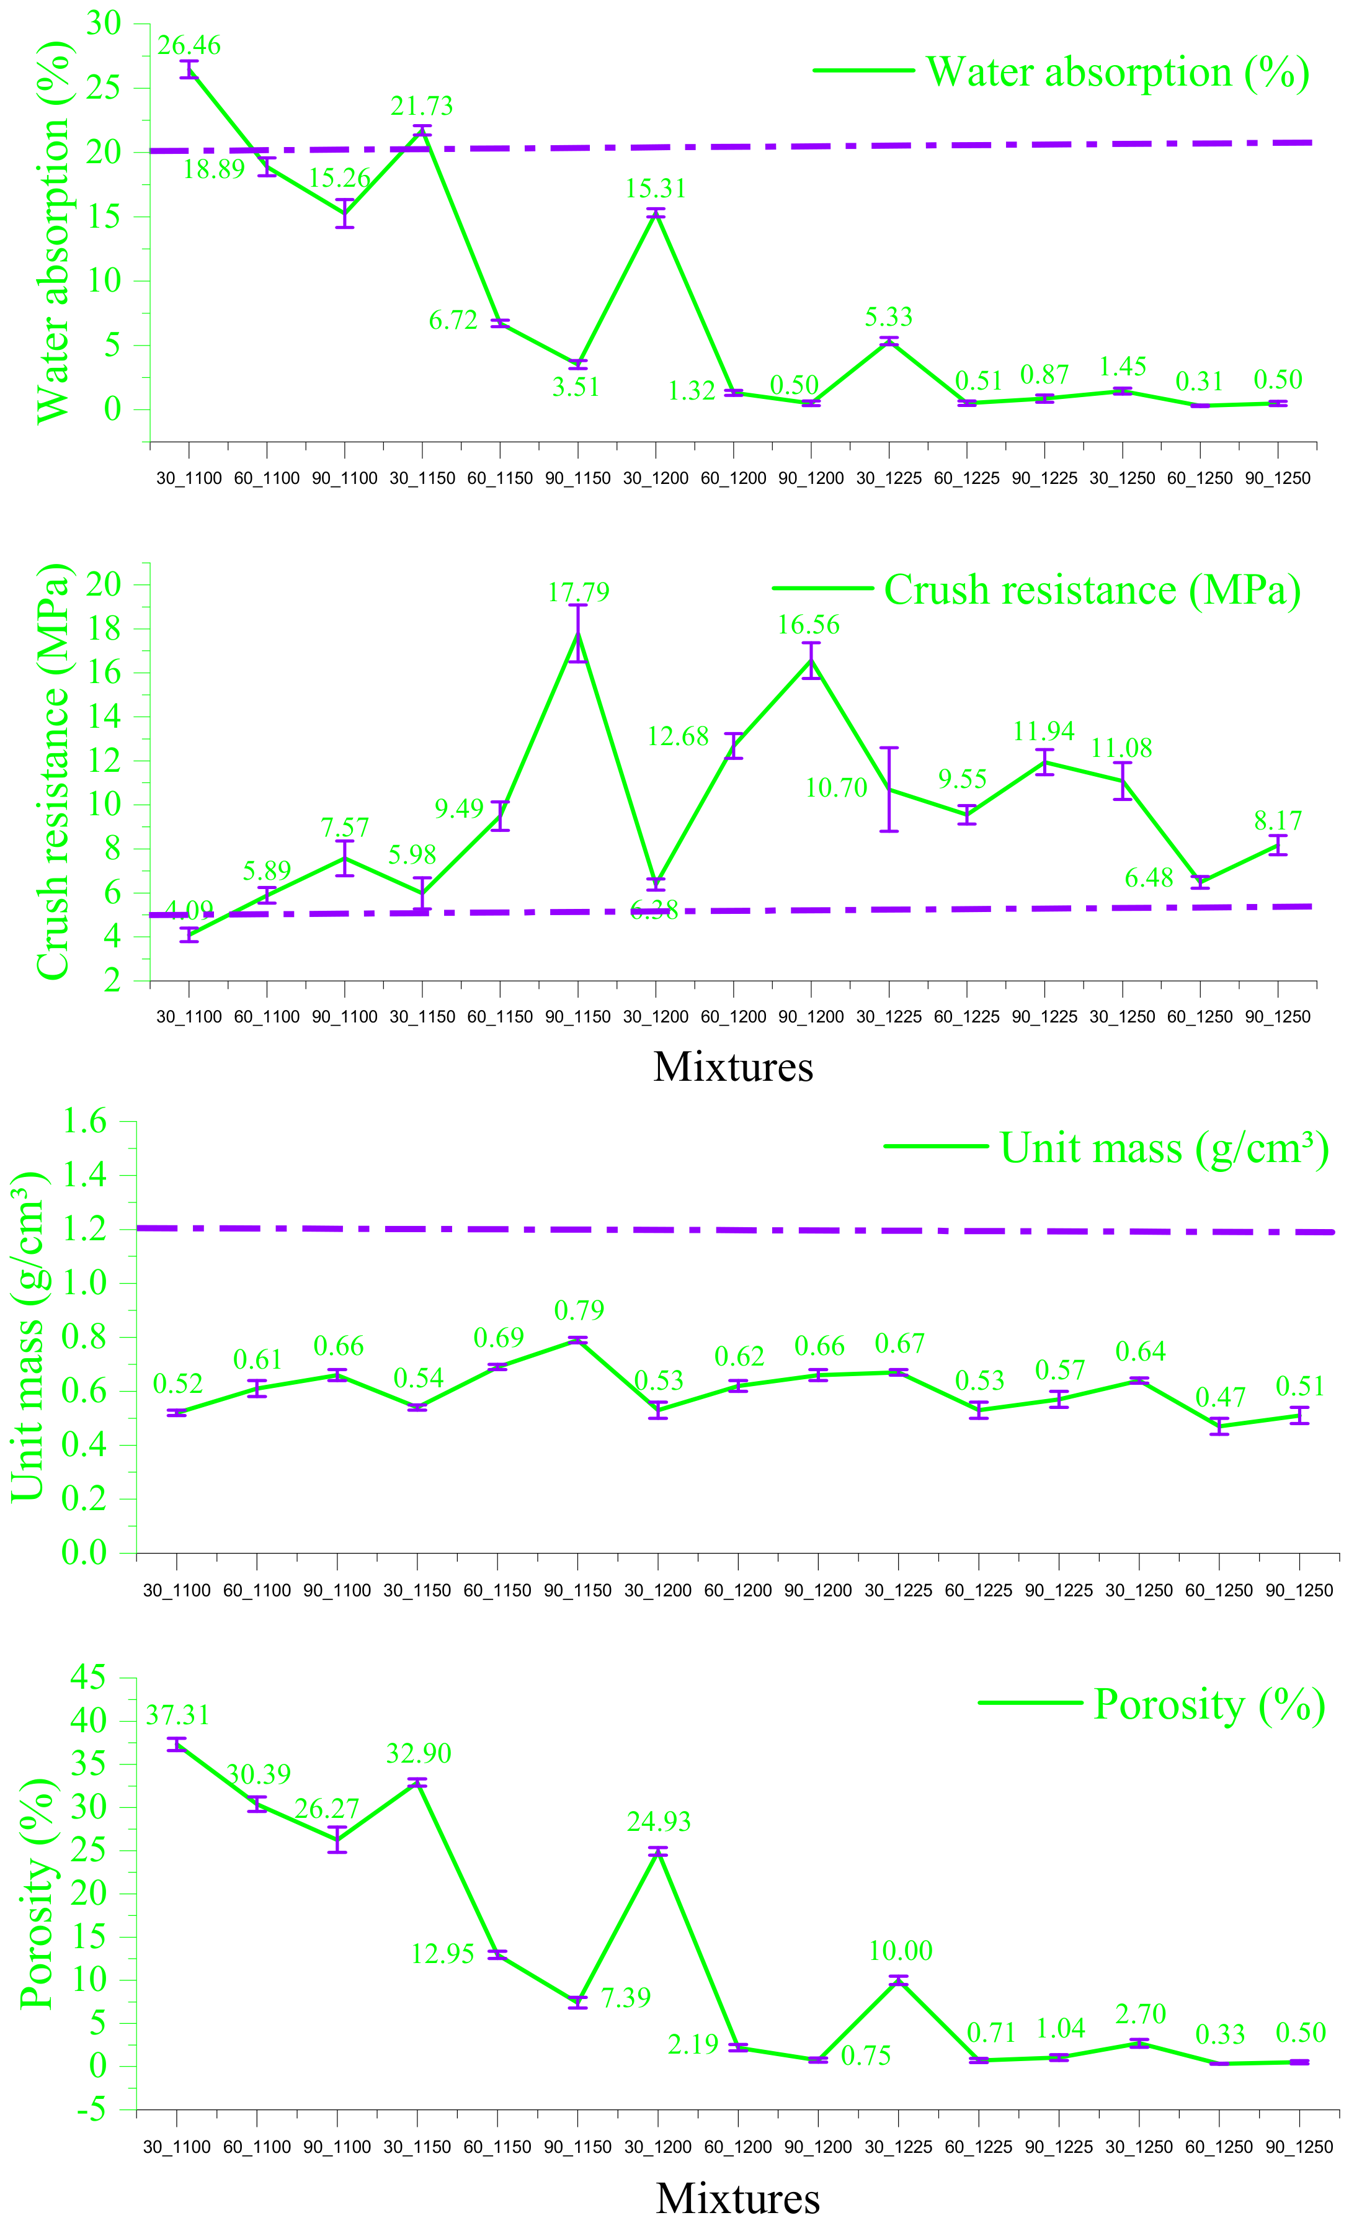
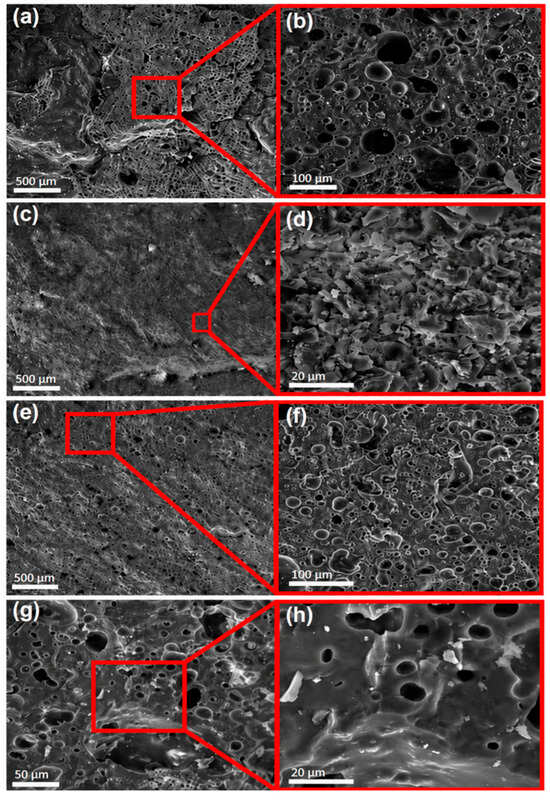
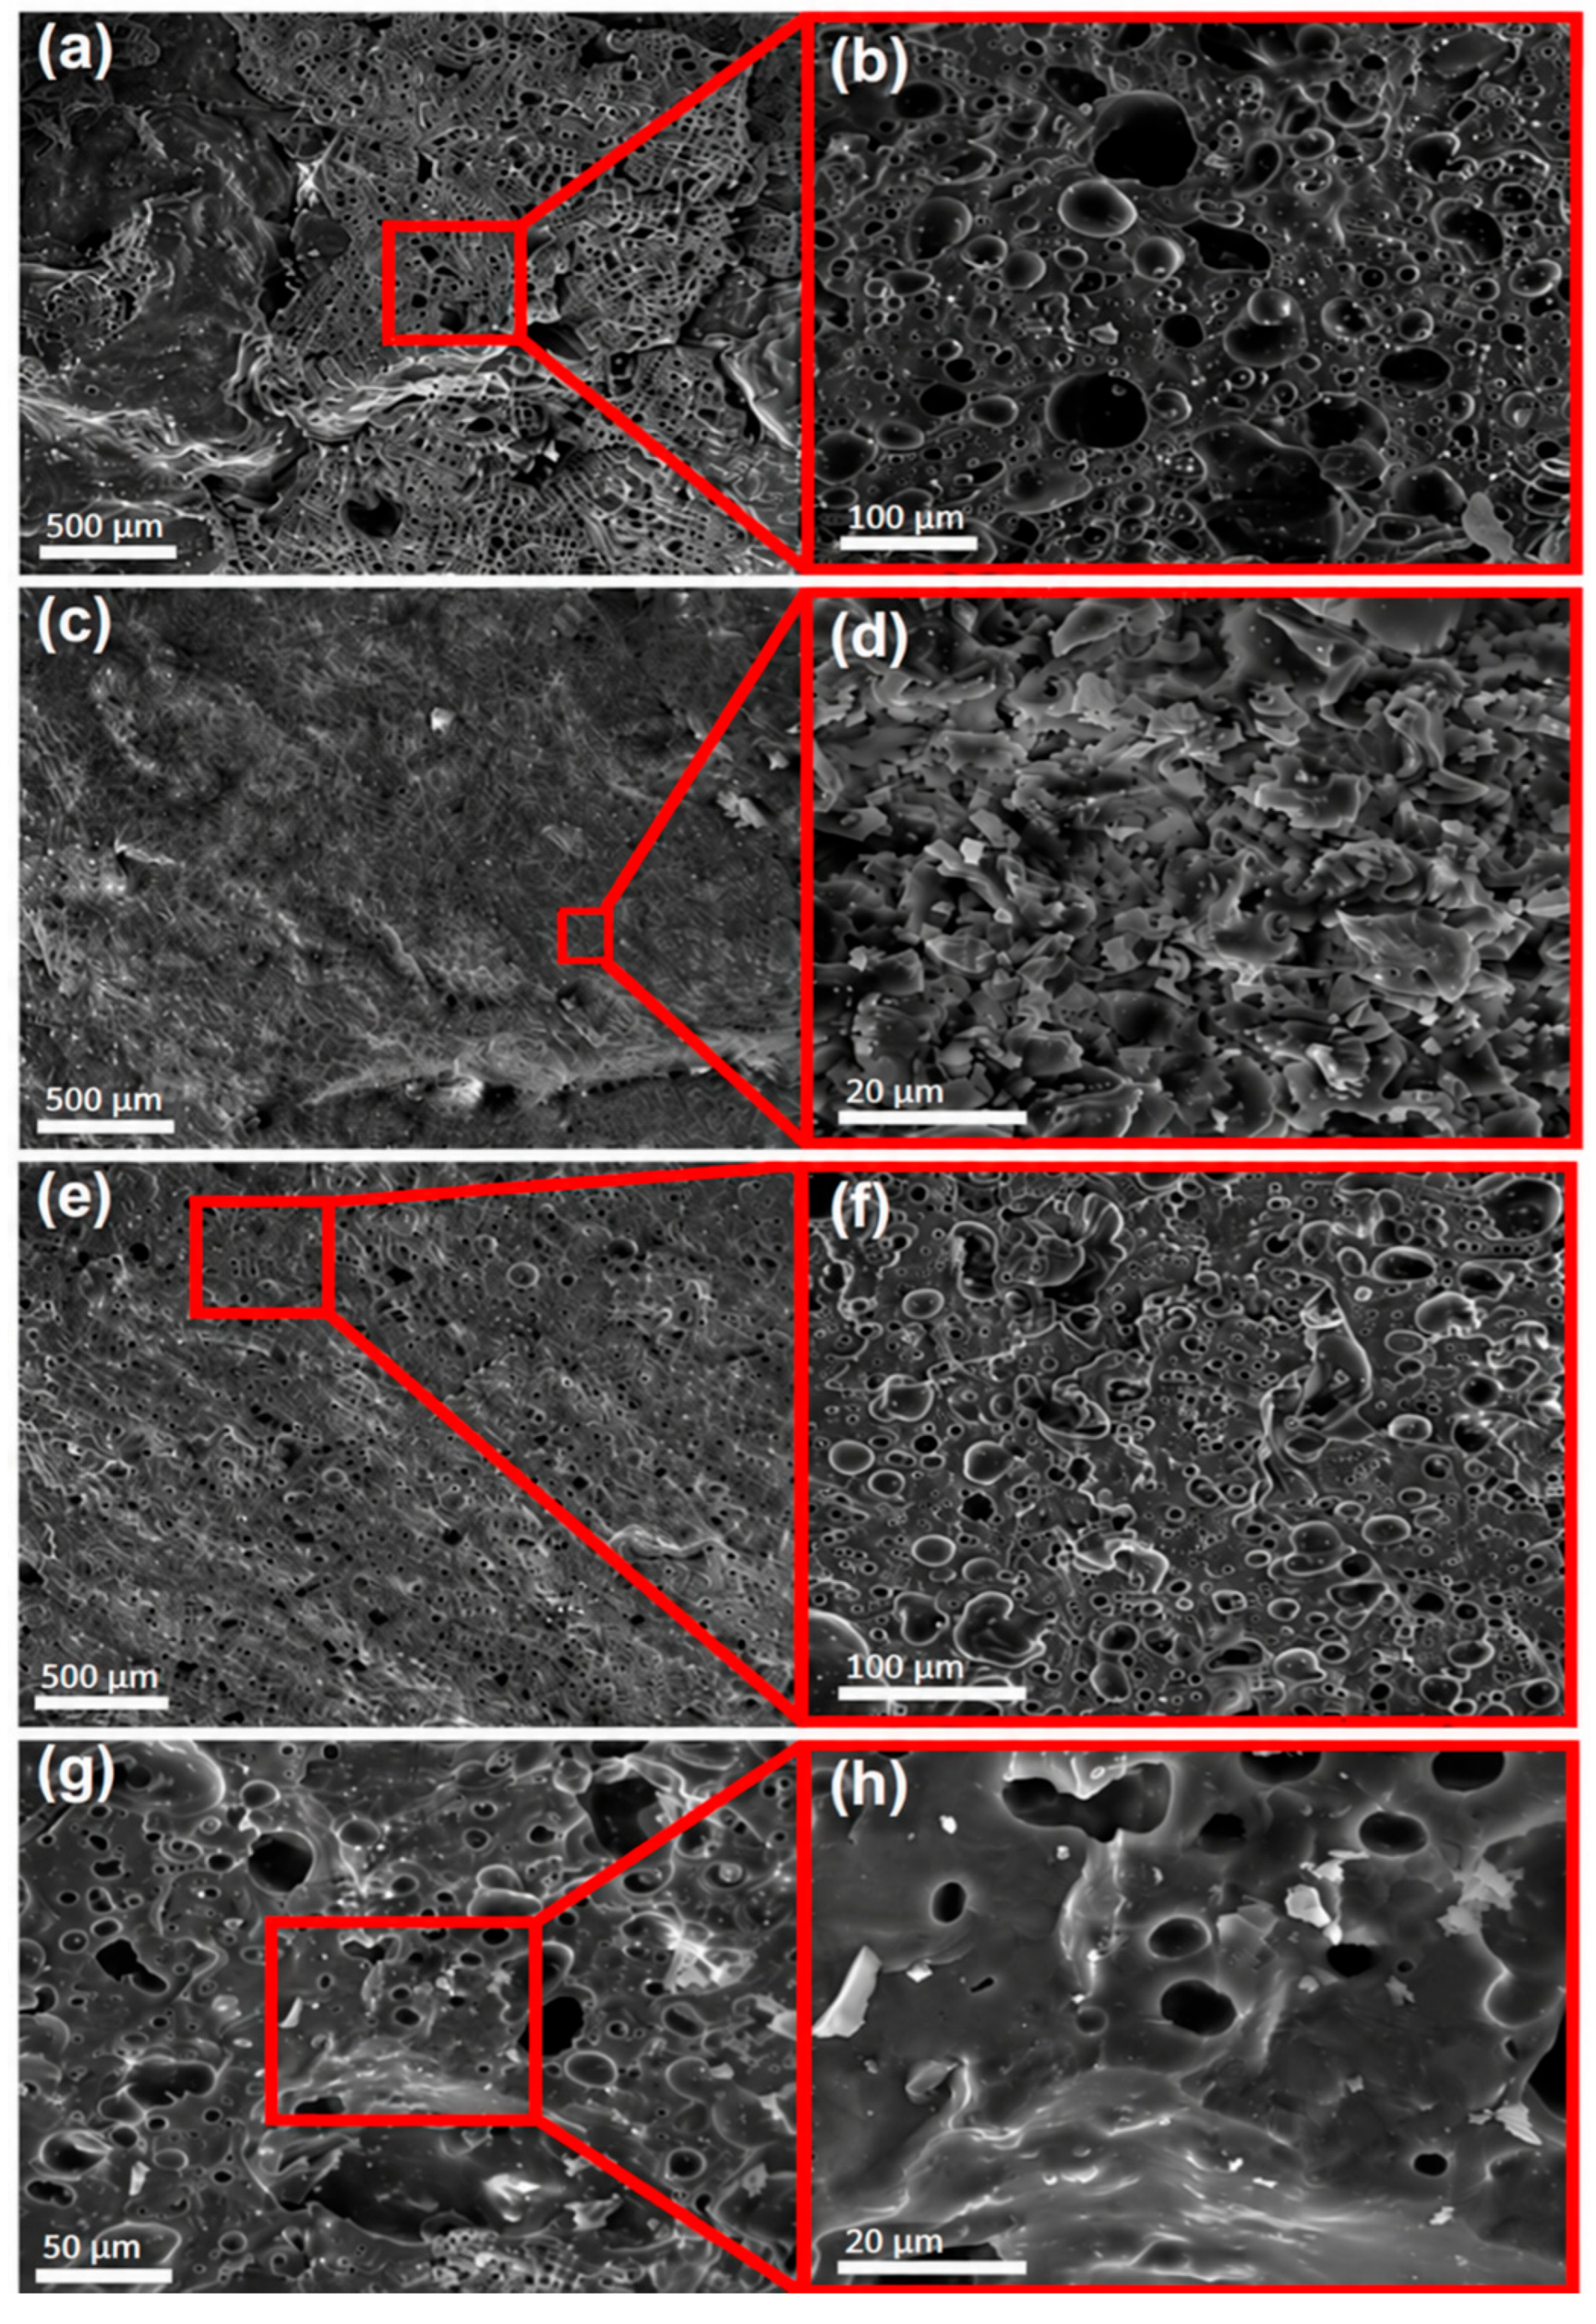
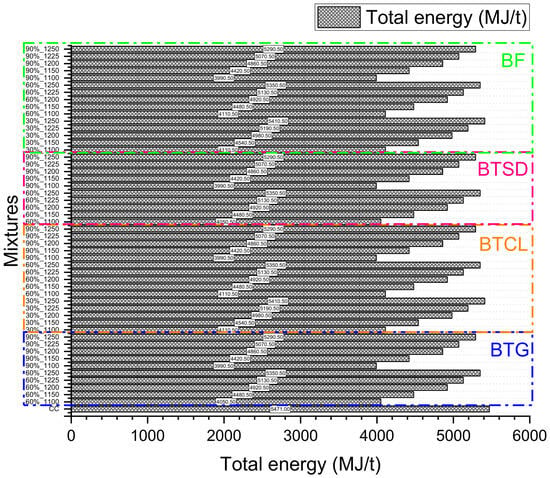
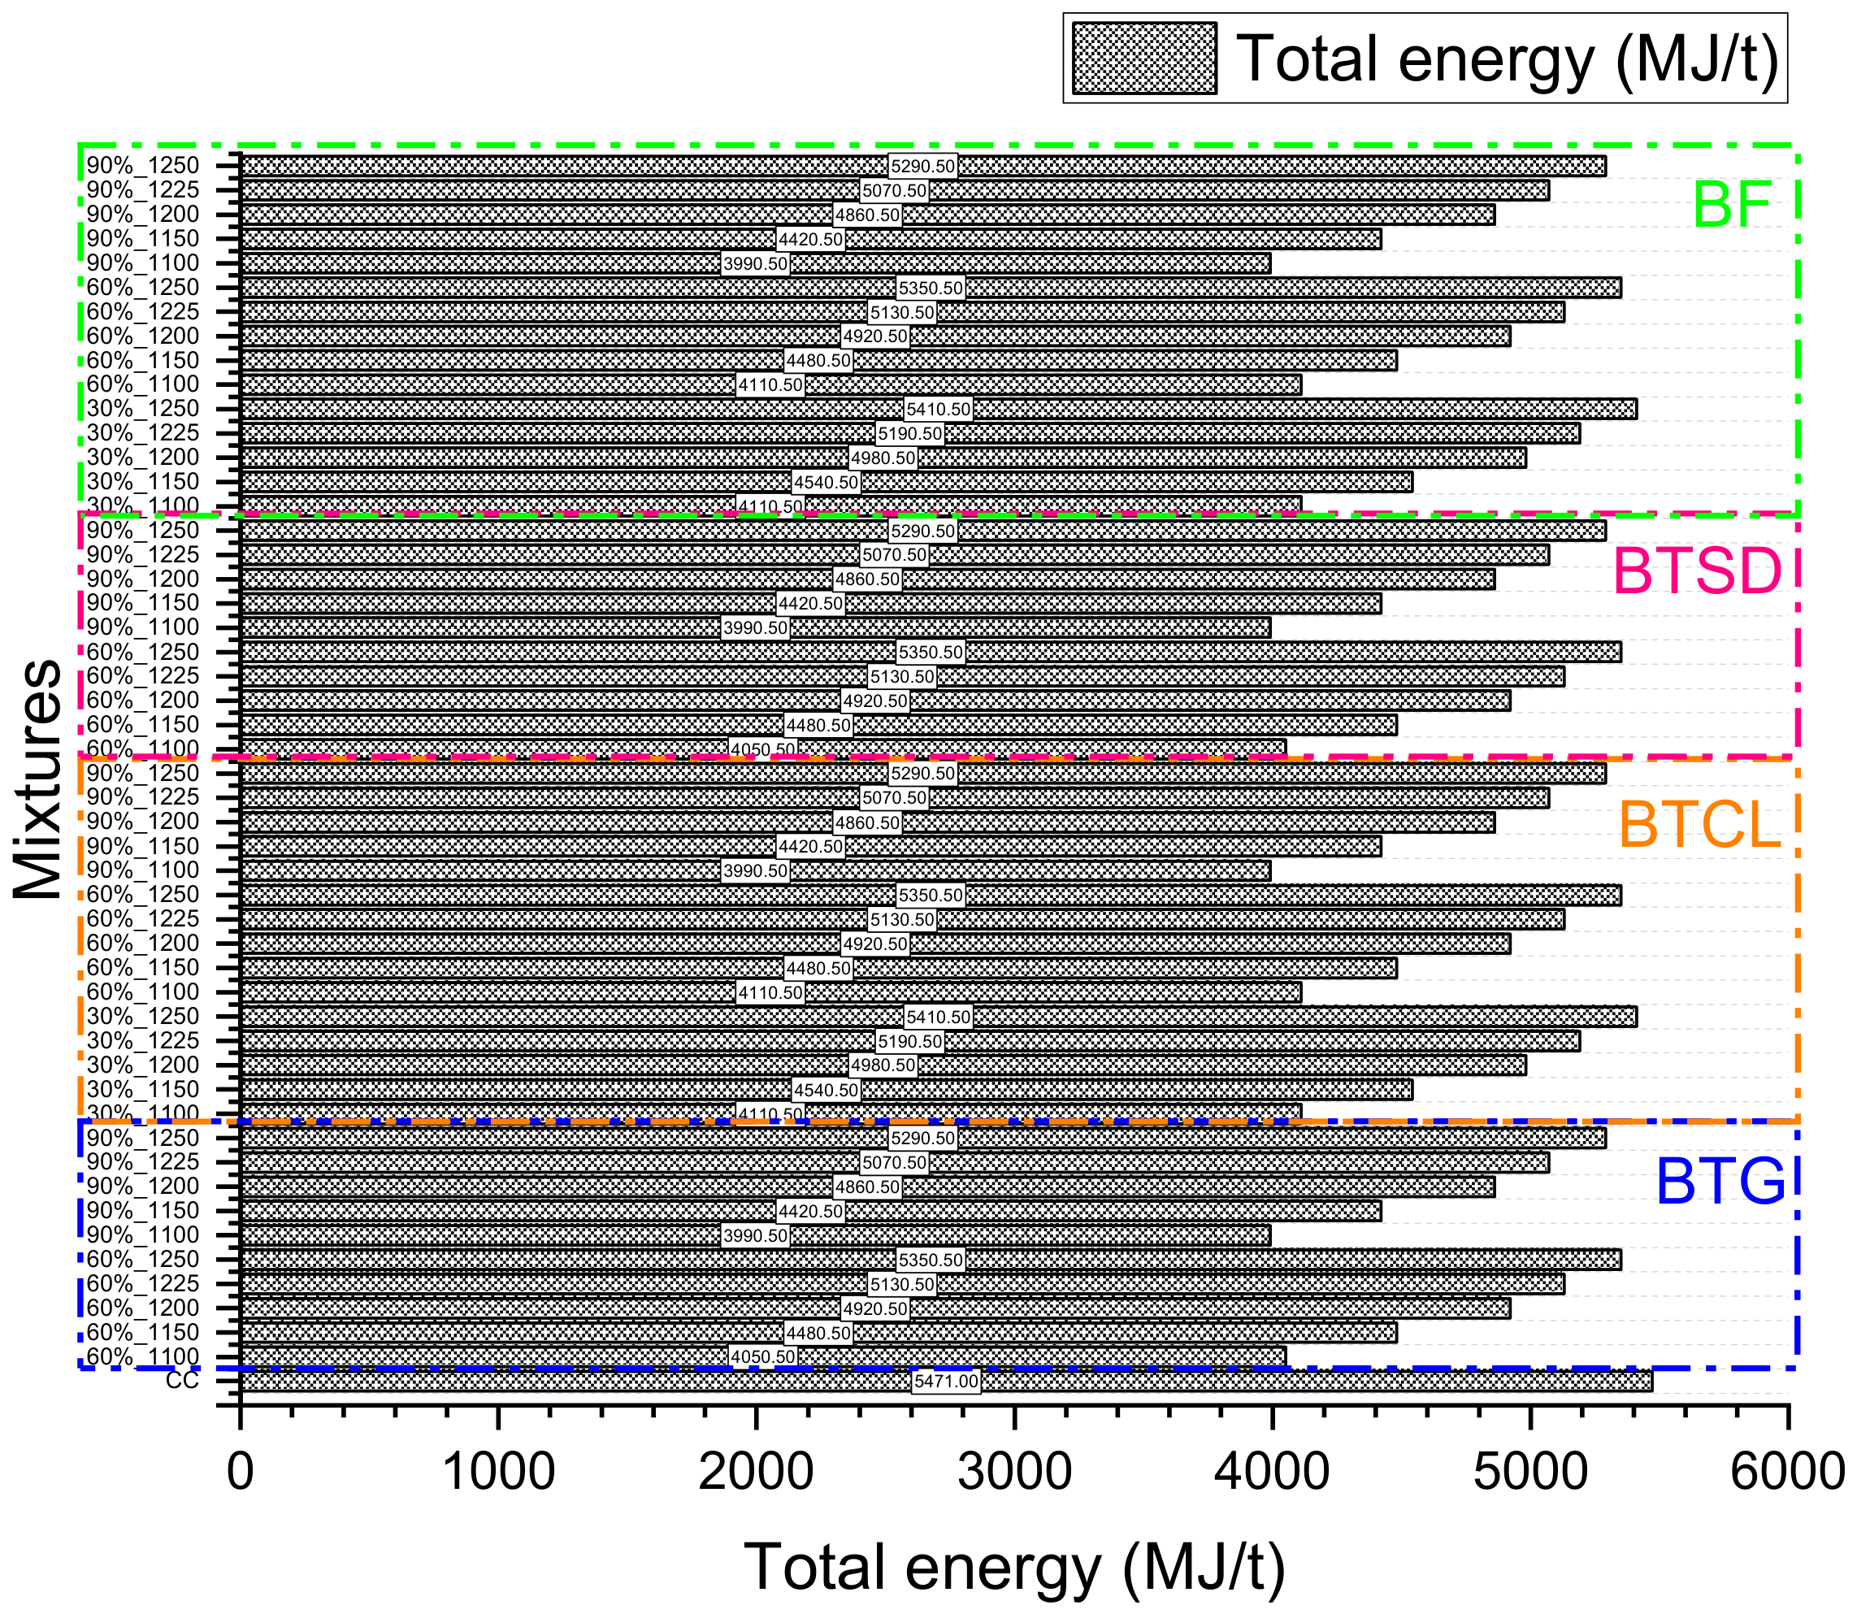
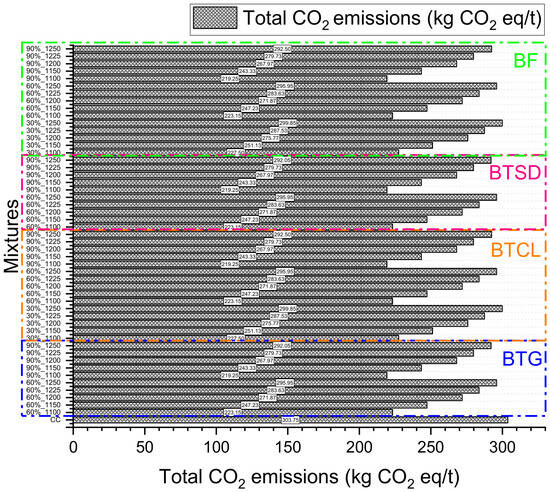
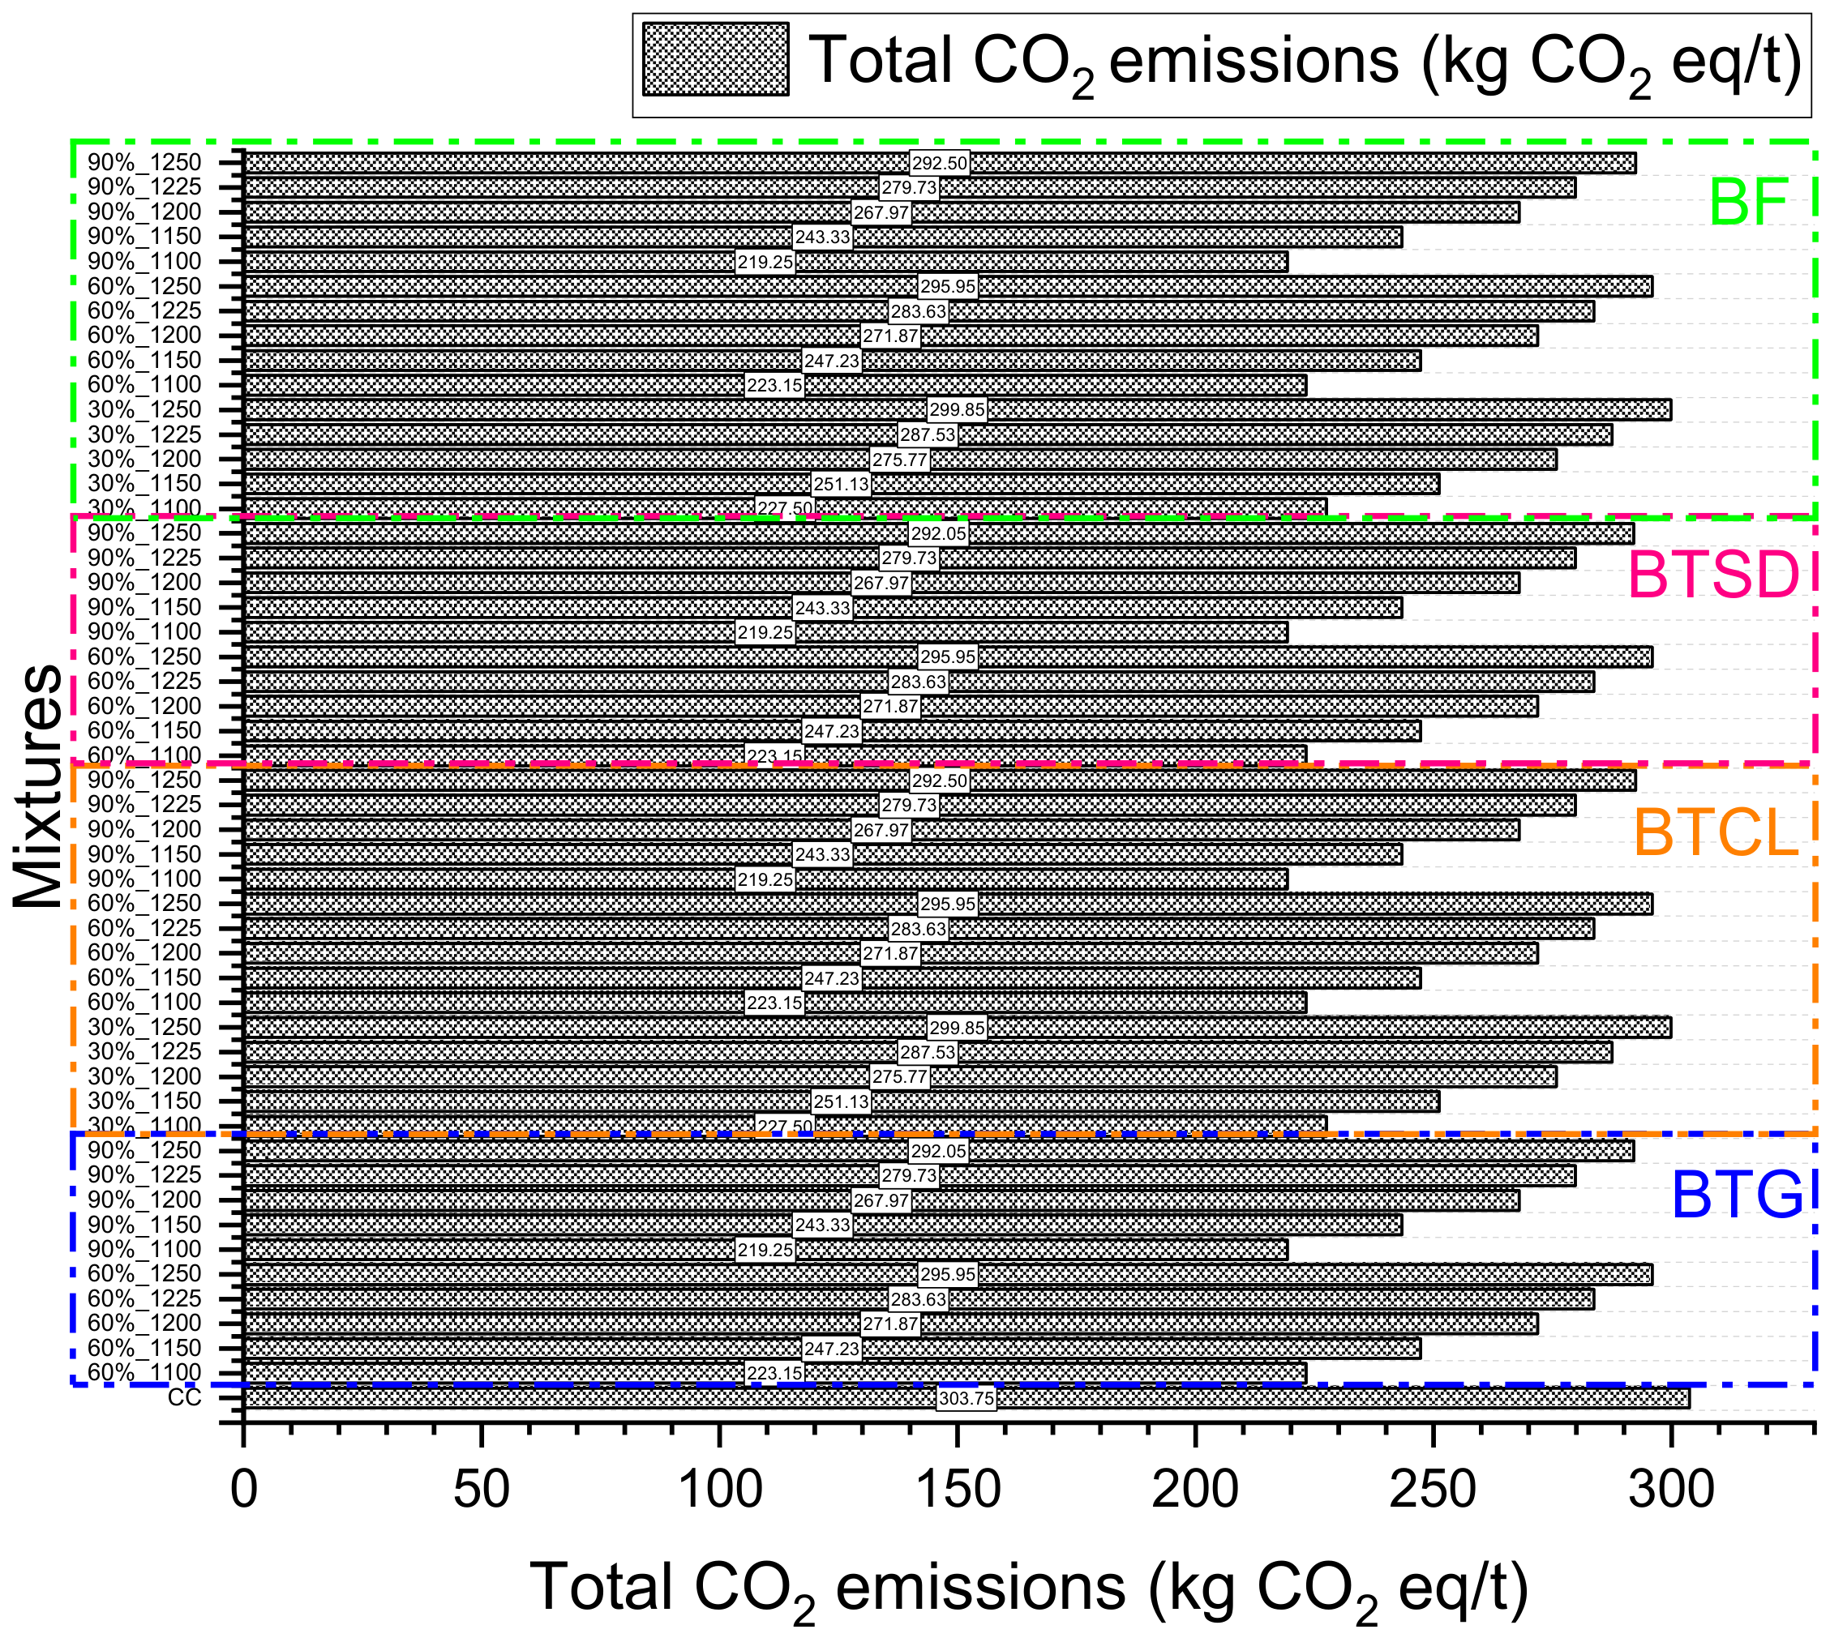
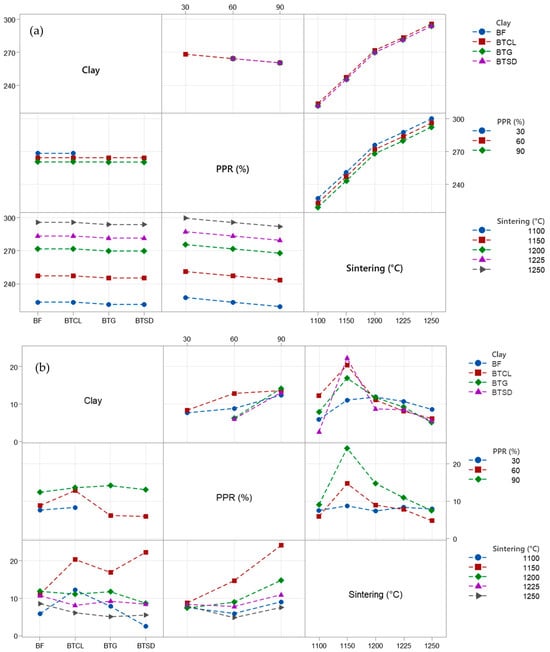
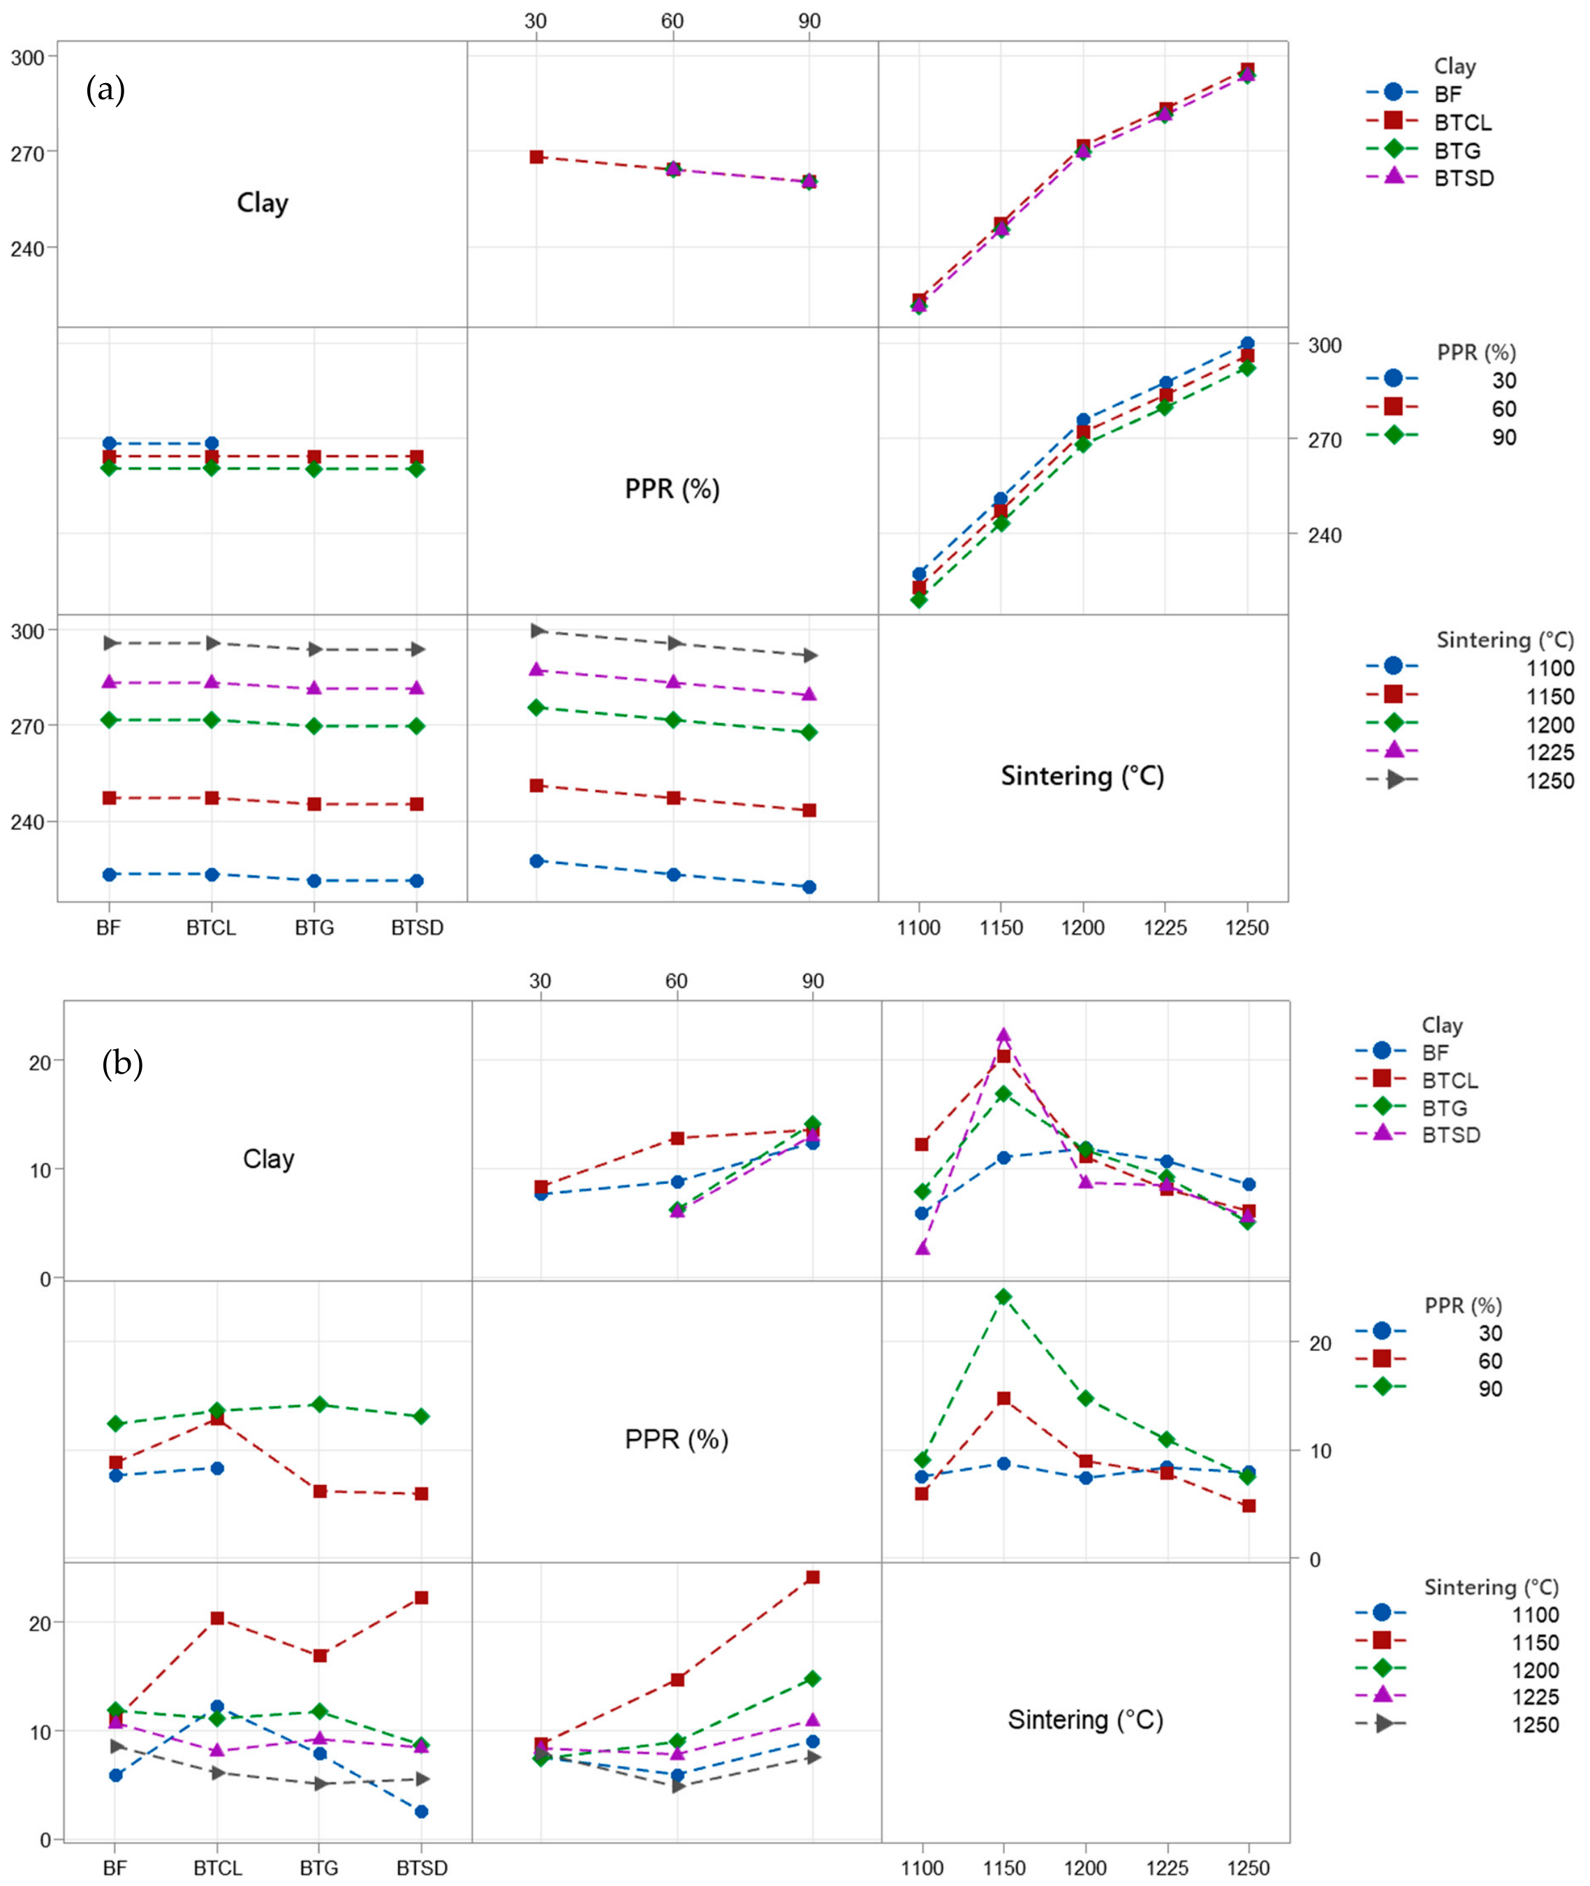
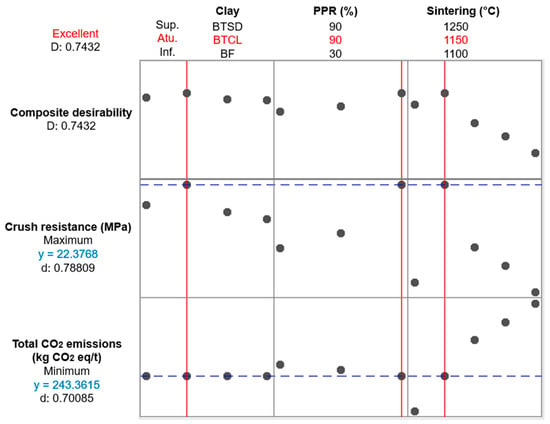
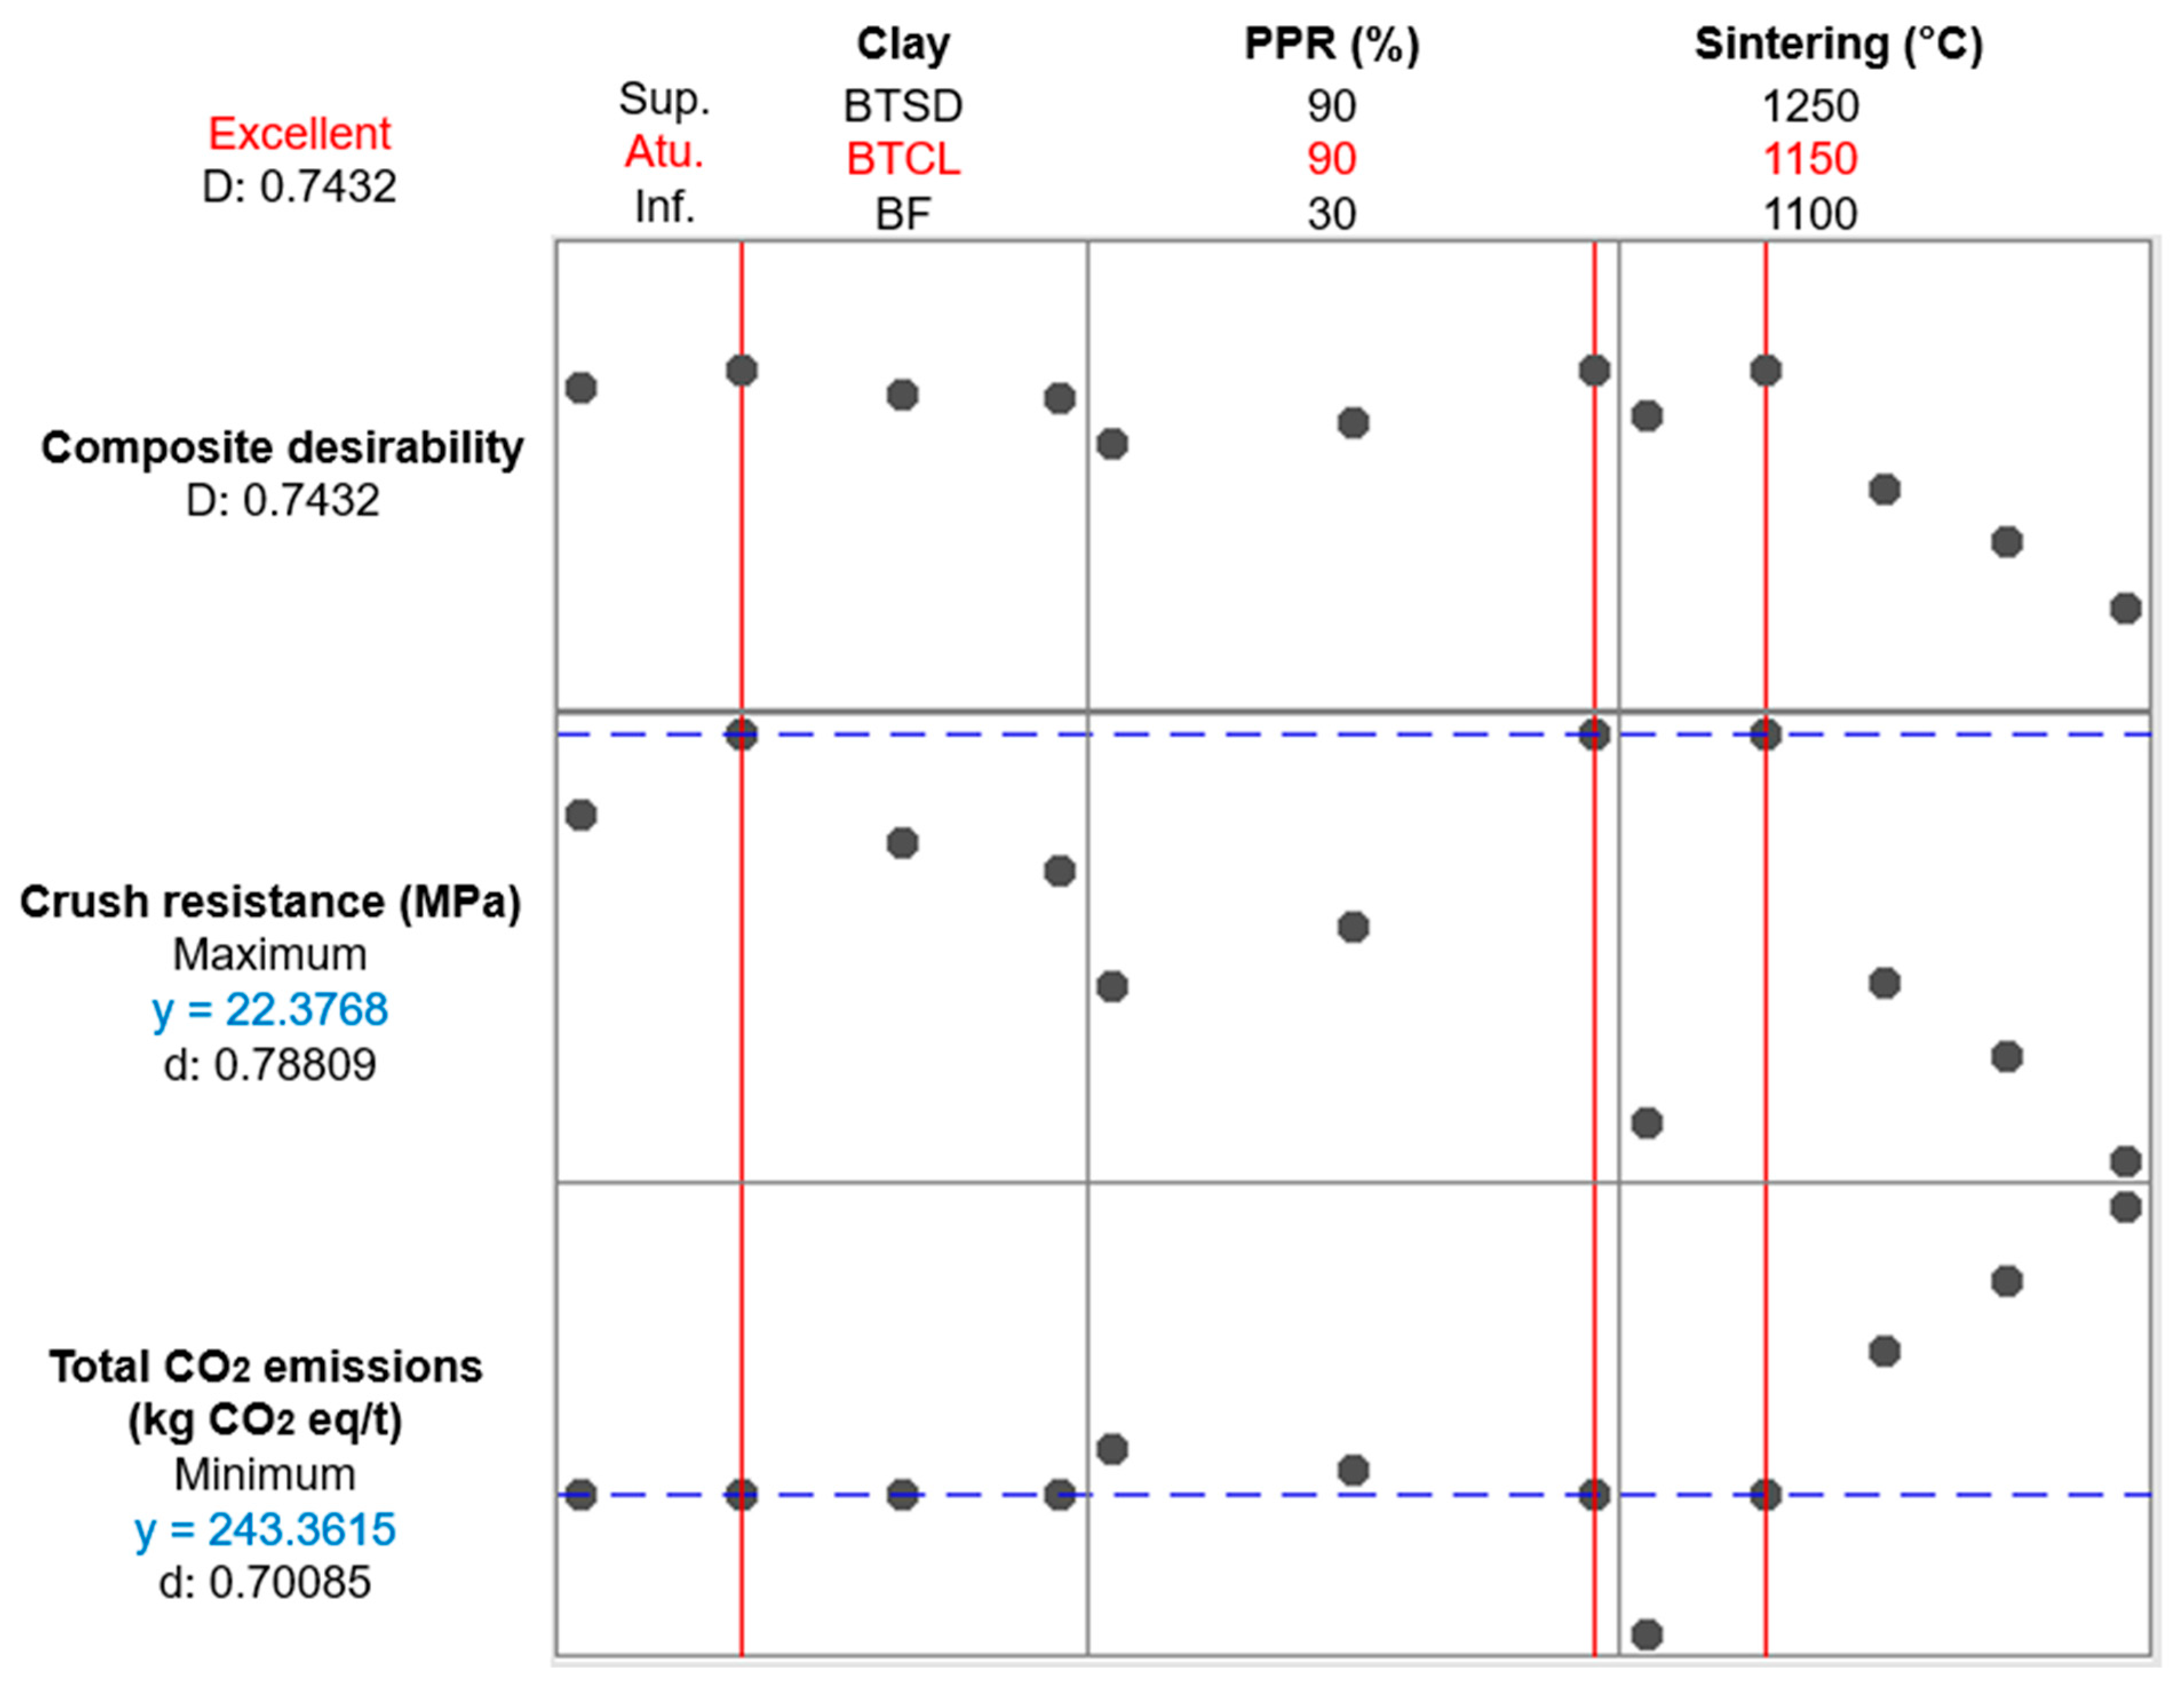

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.