


Abstract
This study investigates the development of high-strength biofiber cement boards with enhanced thermal insulation properties by utilizing recycled biofibers derived from cement packaging bags, combined with a water-based adhesive to enhance the curing efficiency of Portland cement through a cementation–curing process. This approach reduces waste from cement packaging and other biofiber residues through recycling, thereby promoting environmental sustainability. Moreover, it does not require the use of additional chemicals for the disposal or treatment of fiber waste, nor does it require the incineration of biofiber waste. Recycled biofiber from cement bags, composed primarily of cellulose (60 wt%), lignin (15 wt%), and hemicellulose (10 wt%), serves as a reinforcing phase, while the cement and adhesive mixture functions as a strong binding matrix. The fabrication of composite materials using undamaged cement bag fibers preserves fiber integrity and enables a well-ordered one-dimensional (1D) fiber alignment, which promotes more effective reinforcement than two-dimensional (2D) or three-dimensional (3D) orientations, in accordance with the rule of mixtures. In addition, the incorporation of a water-based PVAc adhesive accelerates the curing rate of the cement phase, promoting the formation of a strong interconnected network structure, and facilitates a more complete curing process. The physical, mechanical, chemical, and thermal properties of the biofiber cement boards were evaluated in accordance with relevant industrial standards, including TISI 878:2023, BS 874, ASTM C1185, ASTM D570, ASTM C518, ISO 8301, and JIS A1412. The results indicate that an optimal cement mortar to water-based adhesive ratio of 1:2, combined with an increased number of biofiber sheet layers, significantly enhances material performance, particularly in Formulas (7)–(9). Among these, Formula (9) exhibits the lowest water absorption (0.0835 ± 0.0102%), the highest tensile strength (19.489 ± 0.670 MPa), the highest flexural strength (20.867 ± 2.505 MPa), the highest Young’s modulus (5735.068 ± 387.032 MPa), and low thermal conductivity (0.152 W/m.K). The resulting boards demonstrate strong bonding ability, enhanced resistance to fire, moisture, and weathering, and a longer service life compared to lower cement-to-adhesive ratios (1:1 and 1:0). These findings demonstrate the potential of recycled biofiber composites, combined with water-based adhesives, as sustainable alternative materials for thermal insulation and structural applications, including ceilings and walls in building construction.
1. Introduction
The rapid expansion of infrastructure and urbanization has significantly increased global cement demand, particularly in the residential, commercial, and transportation sectors. This growth has led to increased consumption of cement packaging, especially multi-layer paper bags, due to their strength, low cost, and recyclability. However, cement is highly sensitive to moisture, and premature exposure can initiate hydration reactions, reducing performance. Therefore, developing sustainable and moisture-resistant packaging remains a key challenge in the construction industry [1,2,3].
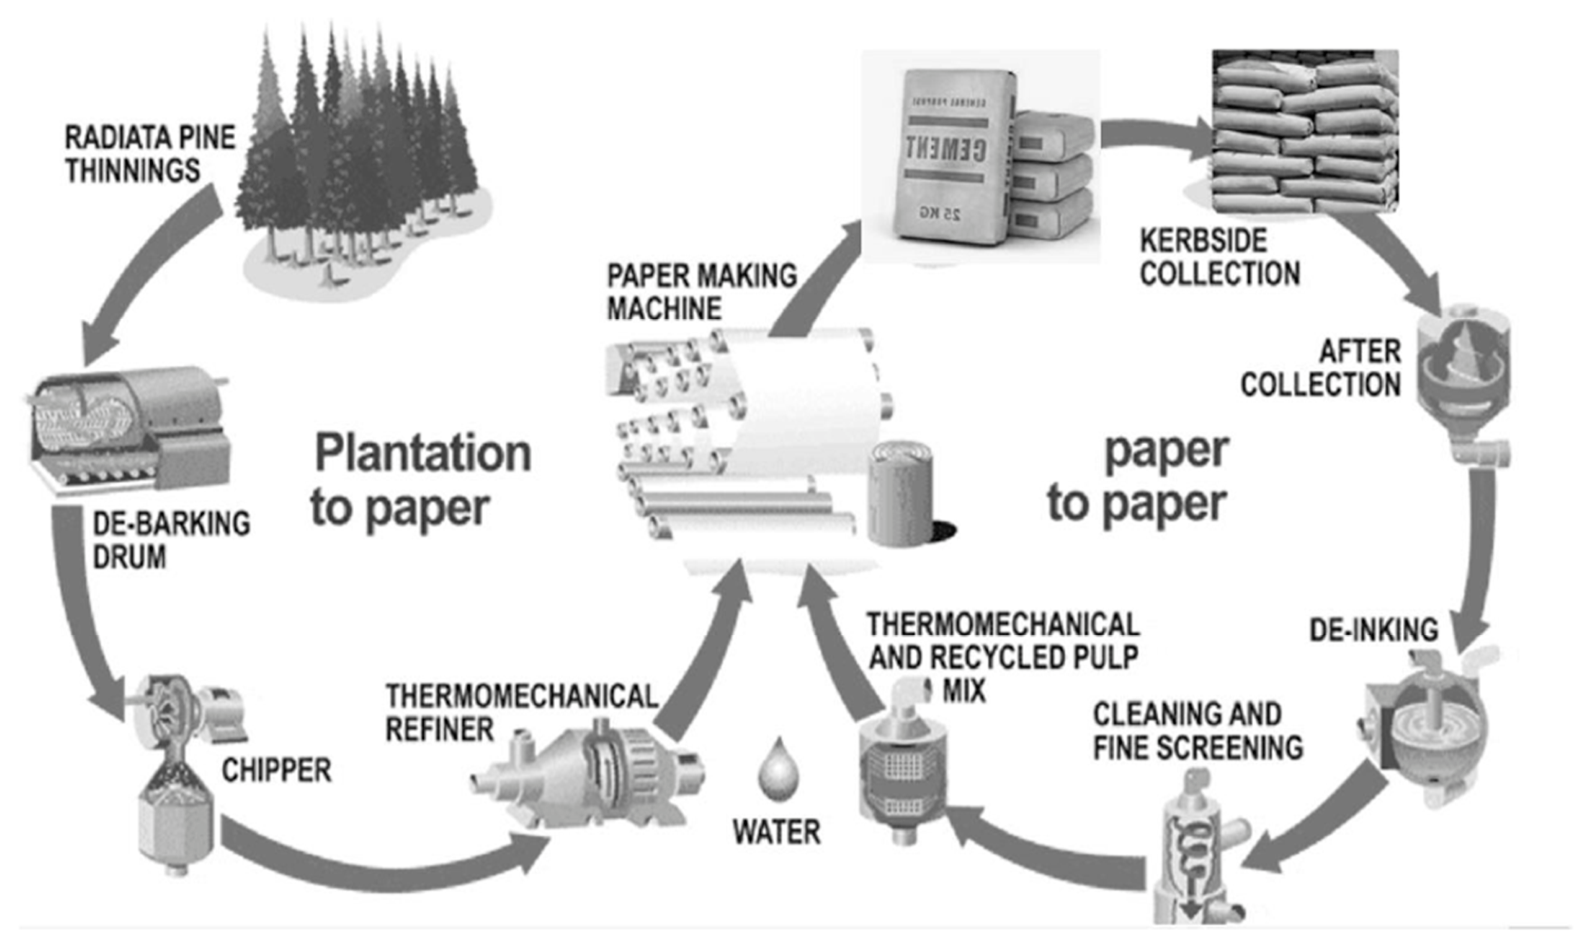
Cement production contributes approximately 7–8% of global CO2 emissions, emphasizing the need for sustainable material solutions. At the same time, large quantities of waste cement packaging and paper-based materials are generated and often disposed of through landfilling or incineration. These wastes consist mainly of lignocellulosic biofibers such as cellulose, lignin, and hemicellulose, which can be recycled into value-added materials. Recycling reduces energy consumption, greenhouse gas emissions, and landfill waste, as illustrated in Figure 1 [4,5,6,7].
Figure 1.
Steps in biofiber manufacturing for industrial use.
Recent studies have demonstrated that recycled lignocellulosic materials can be utilized in construction materials such as insulation panels, lightweight boards, and composites with favorable mechanical and thermal properties [8,9,10,11]. In addition, cellulose-based materials have been widely applied in energy storage, sensors, and smart materials, demonstrating their versatility [12,13,14,15,16]. Biofiber-reinforced cement composites have gained increasing attention due to their sustainability and enhanced performance [17,18,19,20].
Natural fibers exhibit low density, high specific strength, and hierarchical structures, making them suitable for reinforcement in cement composites [21,22,23]. However, their durability in alkaline cement environments remains a challenge due to fiber degradation, requiring optimized design strategies [24,25,26].
Various construction materials such as cement, glass, gypsum, polymers, and fiber composites exhibit different thermal and mechanical properties, as summarized in Table 1 [10]. Cement-based materials are widely used due to their high compressive strength but suffer from brittleness and low tensile strength. To overcome these limitations, fiber reinforcement and polymer modification have been introduced [27,28,29].
Table 1.
Standard values for thermal conductivity and physical and mechanical properties of building materials [2,30,31,32,33,34,35,36].
Cement hydration plays a critical role in mechanical performance. The reaction can be expressed as
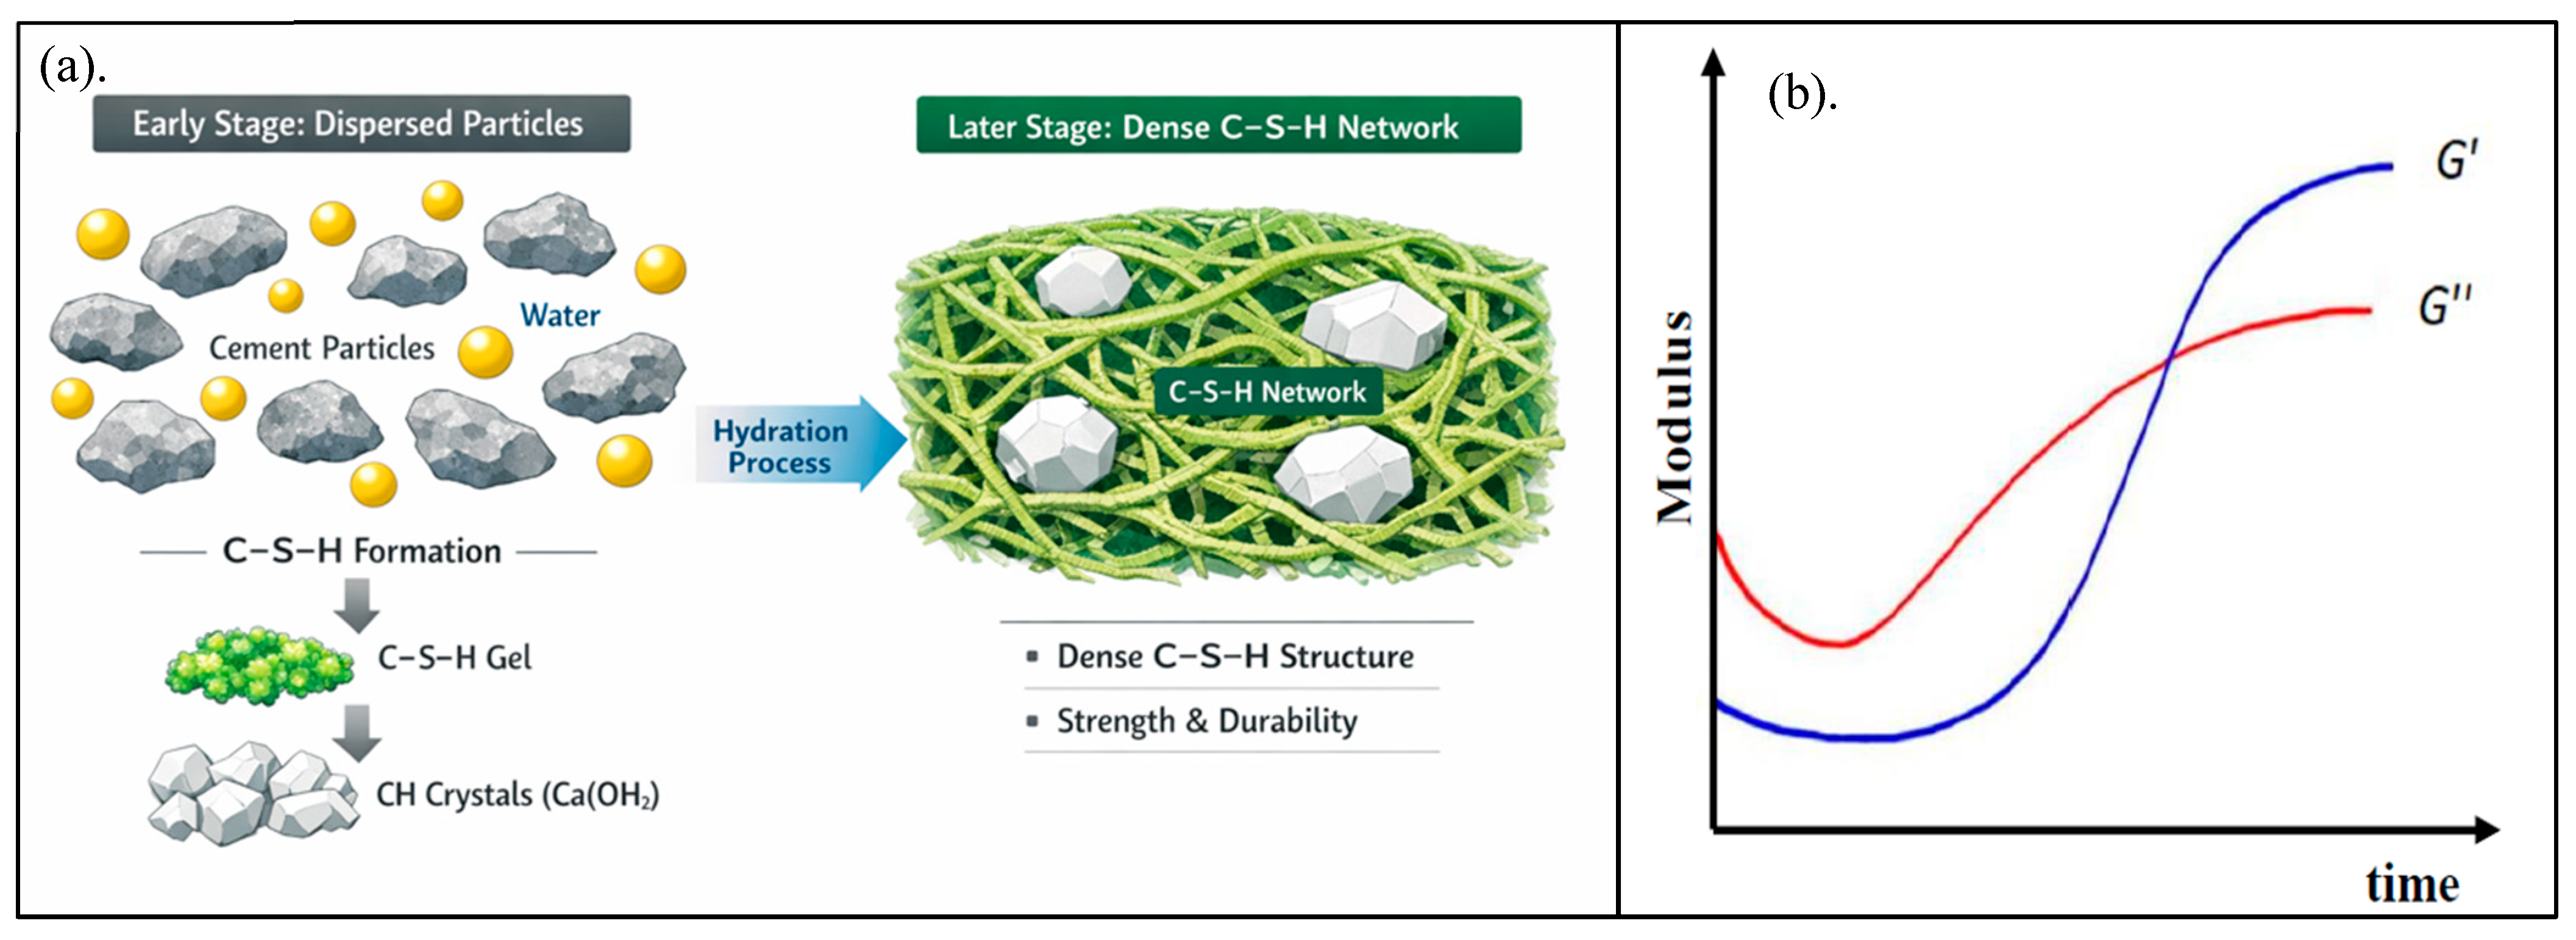
Cement is a widely used binding material in construction due to its adhesive and cohesive properties. As illustrated in Figure 2a, the cohesive structure of hardened cement contributes to its strength, influencing the storage modulus and loss modulus during the accelerated curing process, as shown in Figure 2b. When cement is mixed with water, it forms a hardened matrix through hydration reactions. The curing process contributes to the development of physical (e.g., appearance, color, density, setting time, and shrinkage), mechanical (e.g., compressive, tensile, and flexural strength), and thermal (e.g., conductivity) properties. However, using cement alone can result in excessive rigidity with low tensile strength. To improve flexibility and tensile performance, polymers are often incorporated. There are many types of water-based adhesives, such as polyvinyl alcohol (PVA, [−CH2−CH(OH)−]n); polyvinyl acetate (PVAc, [−CH2−CH(OCOCH3)−]n), commonly known as “white glue”; starch- or dextrin-based adhesives ((C6H10O5)n); and acrylic water-based adhesives ([−CH2−CH(COOC2H5)−]n). When water reacts with cement through hydration, several products are formed: calcium silicate hydrate (C-S-H gel), calcium hydroxide (Ca(OH)2, or portlandite) from silicate hydration, and ettringite or monosulfate from aluminate reactions. For example, combining cement with water-based adhesives or polyvinyl alcohol (PVA) enhances adhesion and tensile properties. Previous studies have reported that incorporating PVA at appropriate polymer–cement ratios can significantly improve the mechanical performance and durability of cement-based composites. Optimal performance is typically achieved at relatively low PVA contents, generally in the range of 0.5–3% by weight of cement, depending on the application and composite design [30,31].
Figure 2.
(a) The cohesive structure of hardened cement contributes to its strength, influencing the storage modulus and loss modulus during the accelerated curing process. (b) The time-dependent evolution of the storage modulus (G′) and the loss modulus (G″) during the curing reaction.
Curing involves the formation of a three-dimensional polymeric network, which enhances durability and performance. Water-based epoxy adhesives are accelerated by the heat generated during cement hydration, eliminating the need for external stimuli such as UV radiation. This dual-curing mechanism transforms the liquid solution into a solid product [32,33]. To achieve complete setting of the water-based adhesive, it is generally necessary to increase the process temperature after gelation. Changes in viscosity and the extent of the curing reaction can be effectively monitored by measuring the elastic moduli, namely the storage modulus (G′) and the loss modulus (G″). As shown in Figure 2b, the evolution of G′ and G″ over time provides insight into the curing process. During the initial (induction) stage, both moduli increase with a noticeable change in slope. At a certain point, G′ and G″ intersect, after which their increase rates decrease and eventually reach a plateau, indicating completion of the reaction. The degree of curing (α) increases from 0 at the onset of the reaction to 1 upon completion. The slope of the curve varies over time, reaching a maximum approximately midway through the reaction. Accordingly, the curing behavior can be effectively characterized using G′ and G″, as illustrated in Figure 2 [32,33]. The degree of curing (α) is defined in Equation (2).
During the initial (induction) stage, both moduli increase, accompanied by a noticeable change in slope. At a certain point, G′ and G″ intersect, after which their rates of increase diminish and eventually reach a plateau, indicating completion of the reaction.
During crosslinking, an exothermic reaction takes place, and the crosslinking rate is directly proportional to the heat released during the process. The greater the number of bonds formed, the more heat is released. Once the reaction is complete, no additional heat is generated. The degree of curing (α) can be expressed as
where Q represents the heat released up to a specific time s, s is the instantaneous rate of heat release, and is the total amount of heat released when the reaction is complete at time in .
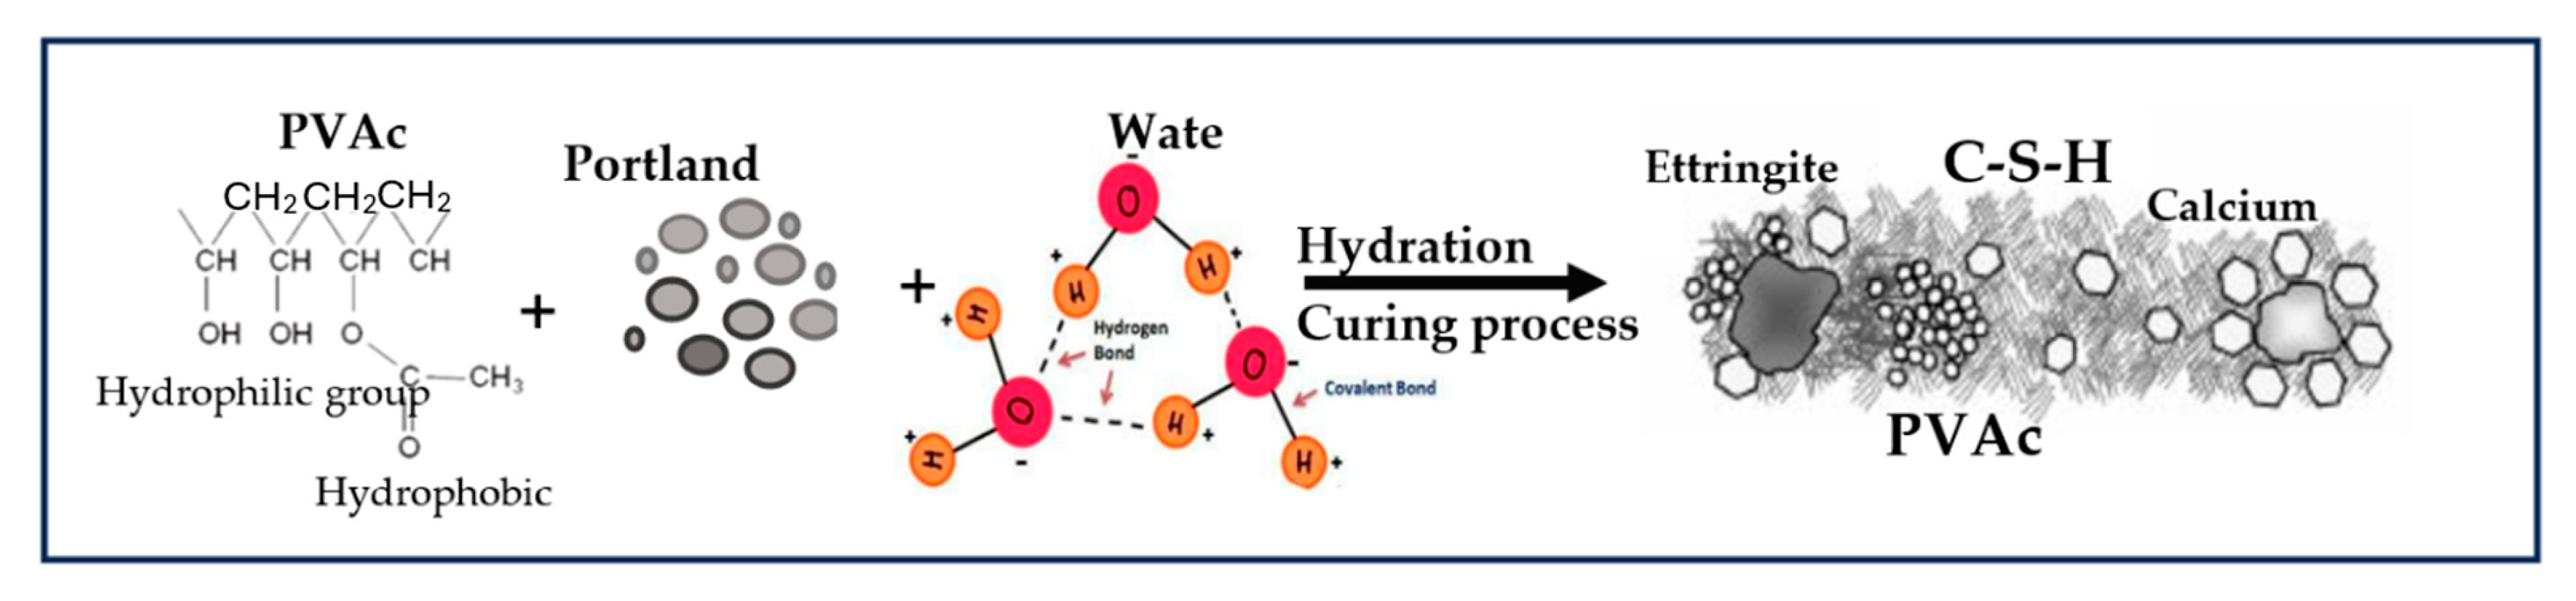
Polymer-modified cement systems have been widely used to improve adhesion and flexibility. Water-based PVAc adhesives enhance bonding through hydrogen bonding and van der Waals forces, forming a three-dimensional network structure (see Figure 3) [34,35,36,37].
Figure 3.
Mechanism of accelerated curing induced by the incorporation of PVAc into Portland cement.
The mechanical performance of fiber composites strongly depends on fiber orientation:
For 1D alignment, , while for 2D and 3D random orientation, and , respectively, resulting in reduced reinforcement efficiency [38,39,40]. Therefore, maintaining fiber alignment is crucial. Additionally, porous fiber structures improve acoustic and thermal insulation due to energy absorption mechanisms [41,42].
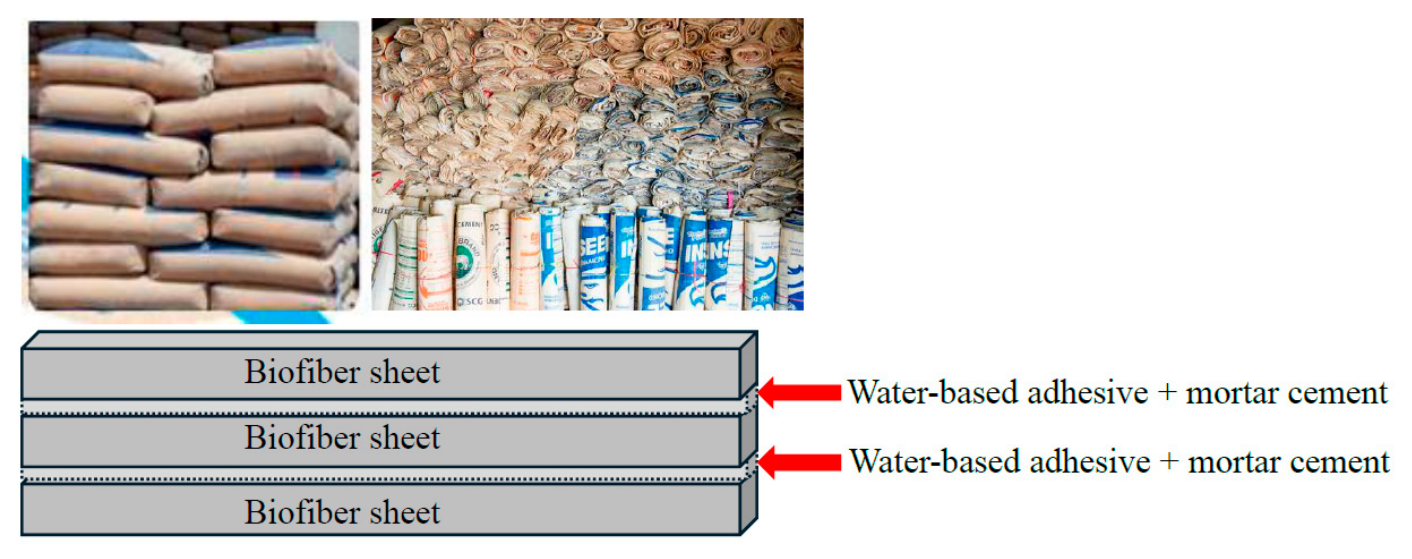
In this study, recycled cement packaging bags were used as biofiber reinforcement without mechanical grinding to preserve one-dimensional fiber alignment and maximize reinforcement efficiency. A multilayer stacked configuration, as illustrated in Figure 4, was employed in combination with a cement–PVAc matrix to form a structural composite. The developed biofiber cement board exhibits improved mechanical strength, reduced density, and enhanced thermal insulation properties. The performance of the samples prepared was evaluated through comparison with standard construction material data, as summarized in Table 1.
Figure 4.
Model of sample preparation.
2. Experimental Section
2.1. Materials
The primary raw materials consisted of 800 sheets of biofibers prepared from locally sourced cement packaging, each cut to dimensions of 7 × 30 cm. A water-based, starch-cellulosic adhesive was supplied by Nan Mee Co., Ltd. (Bangkok, Thailand). The water-based PVAc adhesive, composed of 90–95% deionized water and 6–11% polyvinyl acetate (PVAc, [−CH2−CH(OCOCH3)−]n), is clear and colorless, with a pH of 5–8 and a specific gravity of 1.00–1.06. Portland cement was procured from Jorakay Co., Ltd. (Bangkok, Thailand). Its specifications are as follows: residue on 325-mesh screen ≈ 24%, maximum autoclave expansion 1%, minimum initial setting time 90 min, standard compressive strength 20–30 MPa at 7 days and 65 MPa at 28 days, air content in mortar 8–19% vol, and minimum water retention value 70%.
2.2. Instruments
A paper cutter (model: V-Virgin TS 125/115; manufacturer information unavailable) with a power rating of 540 W and a maximum rotational speed of 12,000 rpm was used to cut the cement packaging sheets.
Non-destructive testing (NDT) was conducted to inspect and evaluate the prepared samples using visual testing (VT). Visual observation, the first assessment method applied, was used to detect cracks, shrinkage, surface quality, and application feasibility in accordance with TISI 878-2023 [43] and BS EN 196-1:2016 [44] standards.
The bulk density of the raw materials was calculated using where is the bulk density (g/cm3), is the sample mass (g), and is the sample volume (cm3), derived from dimensional measurements.
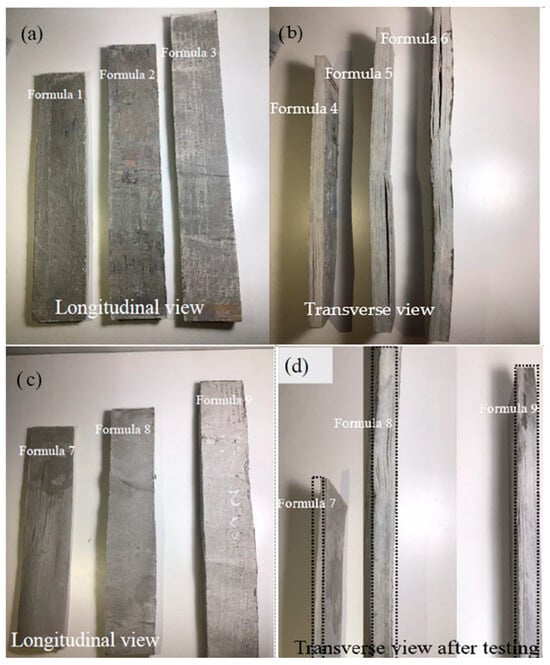
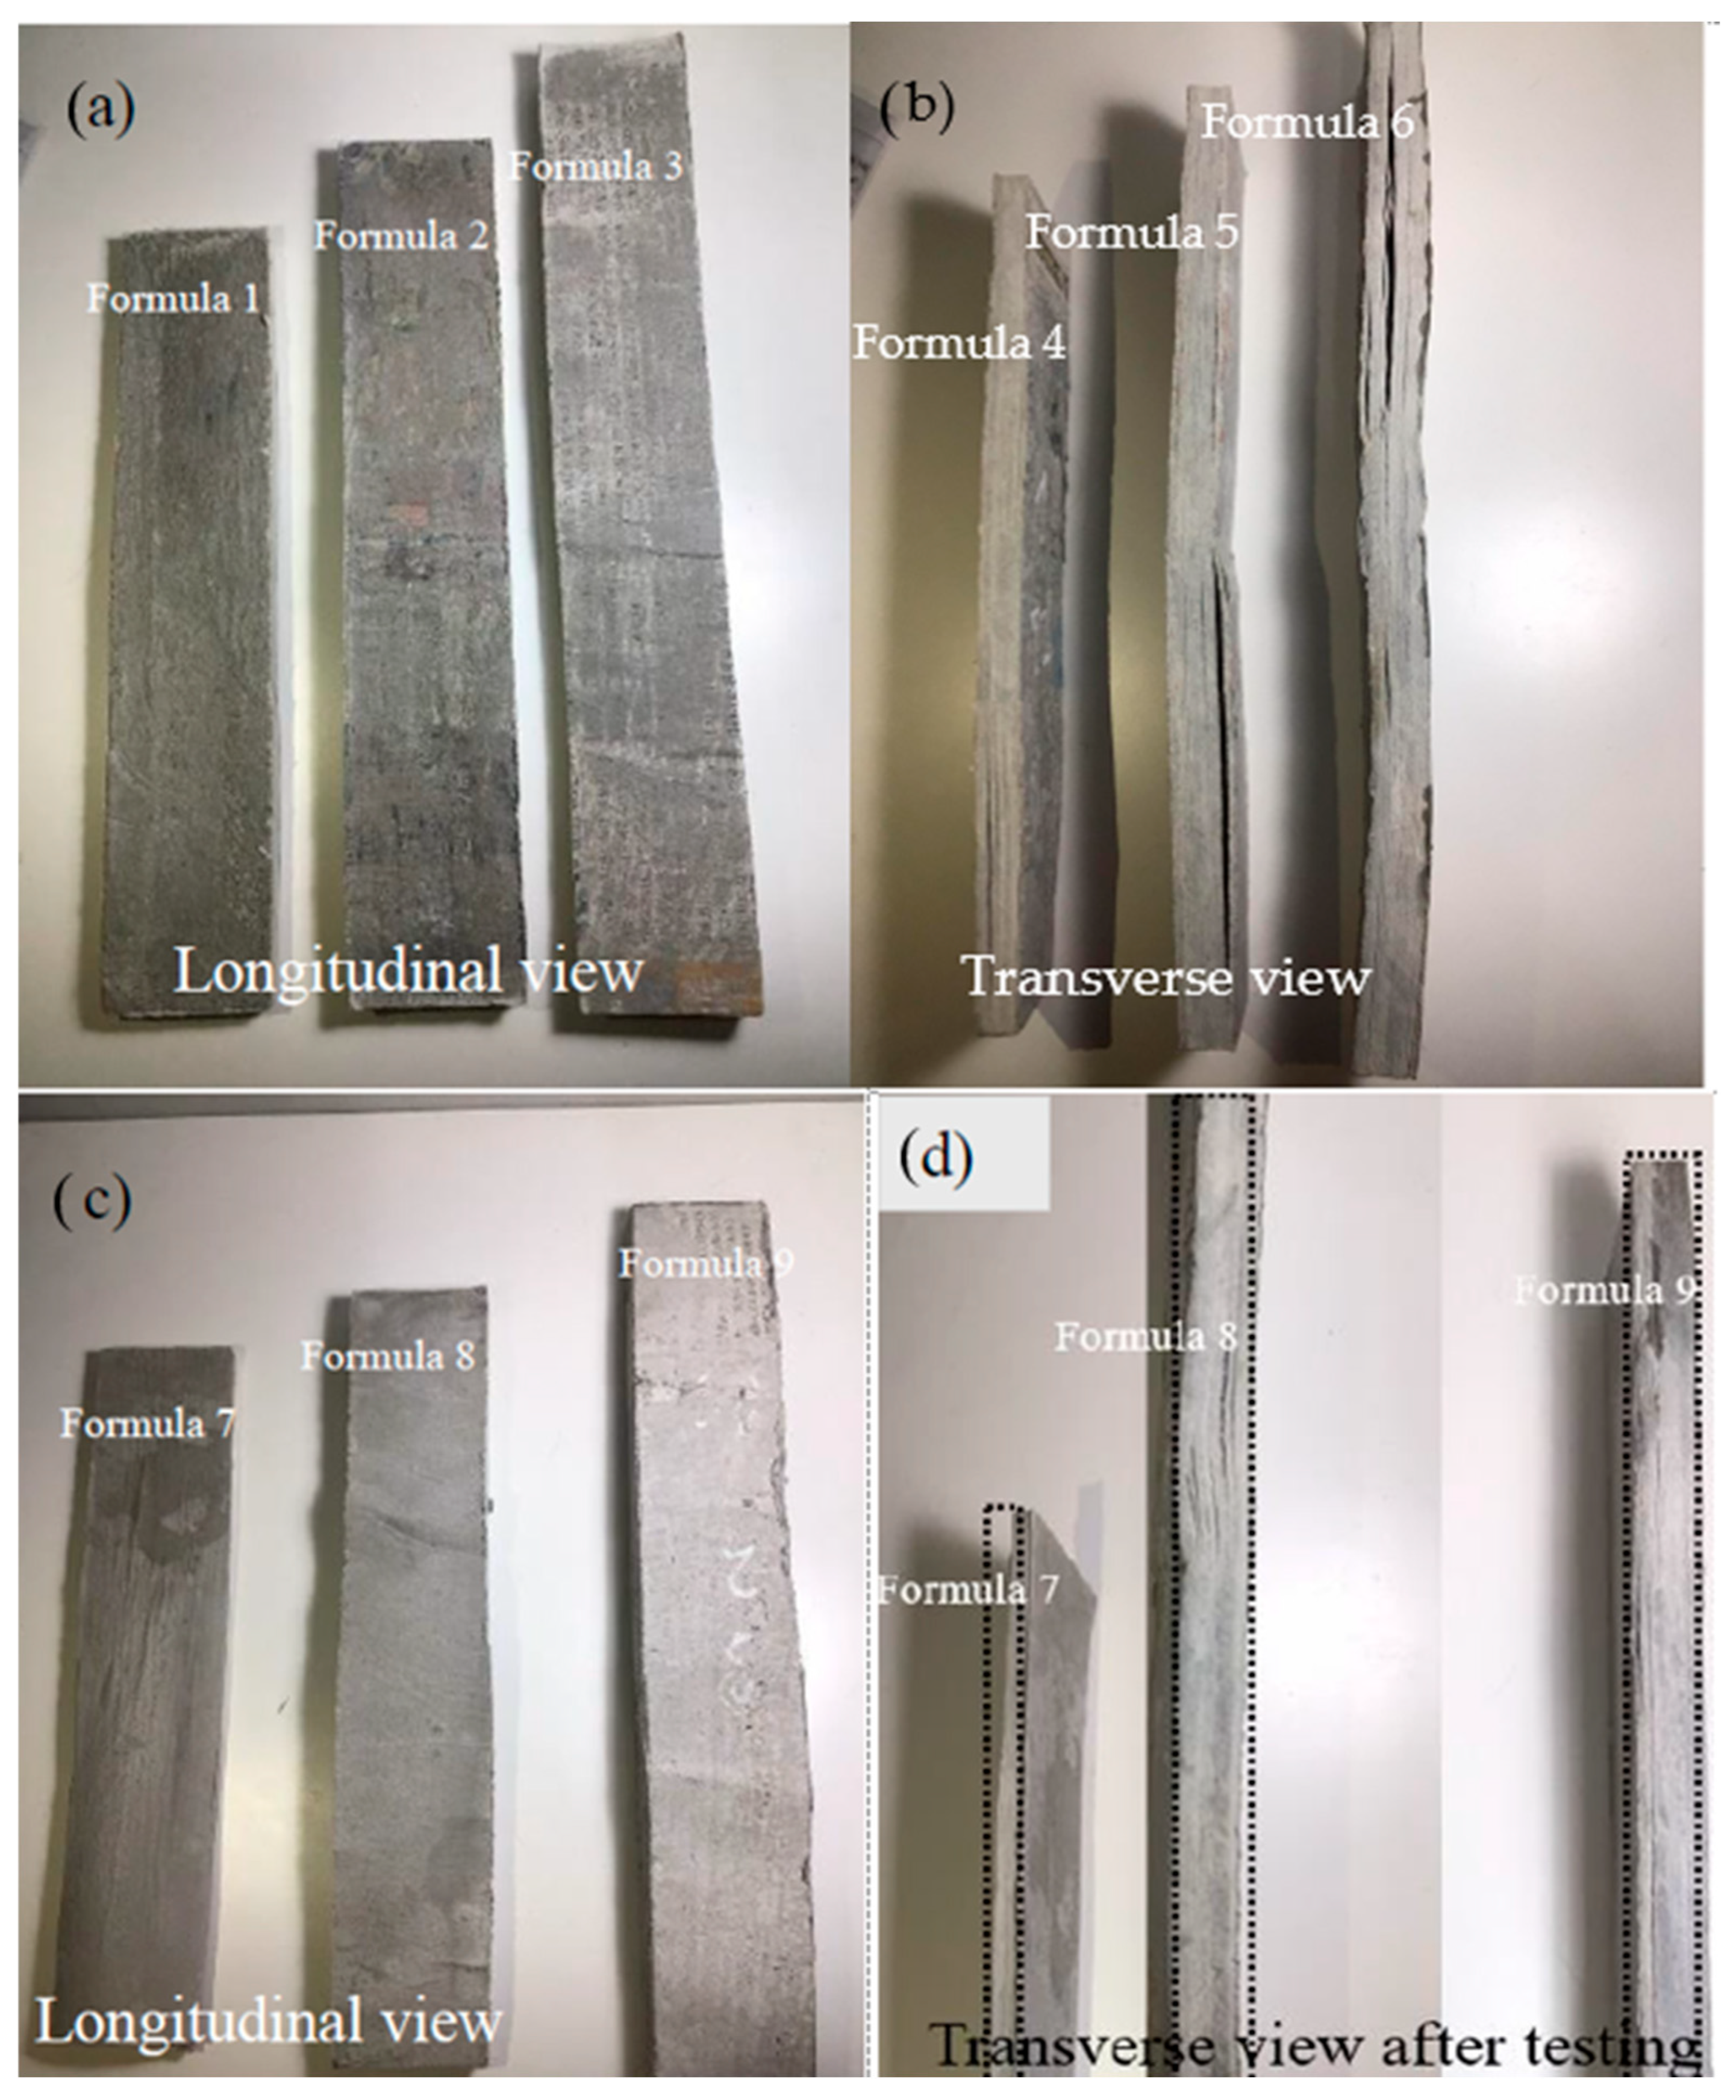
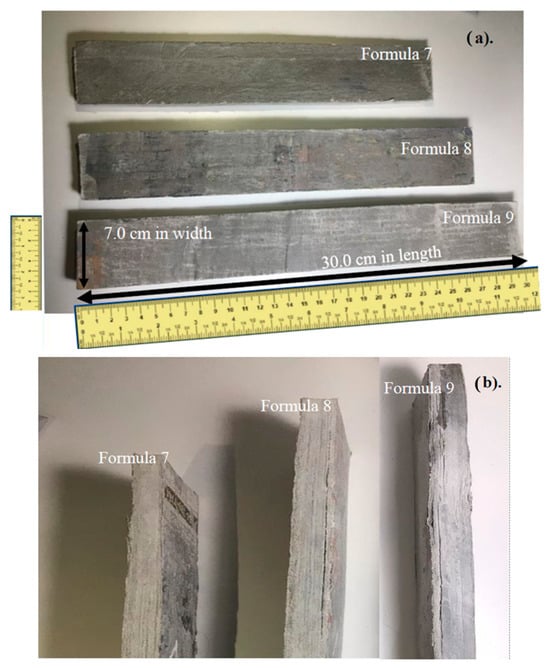
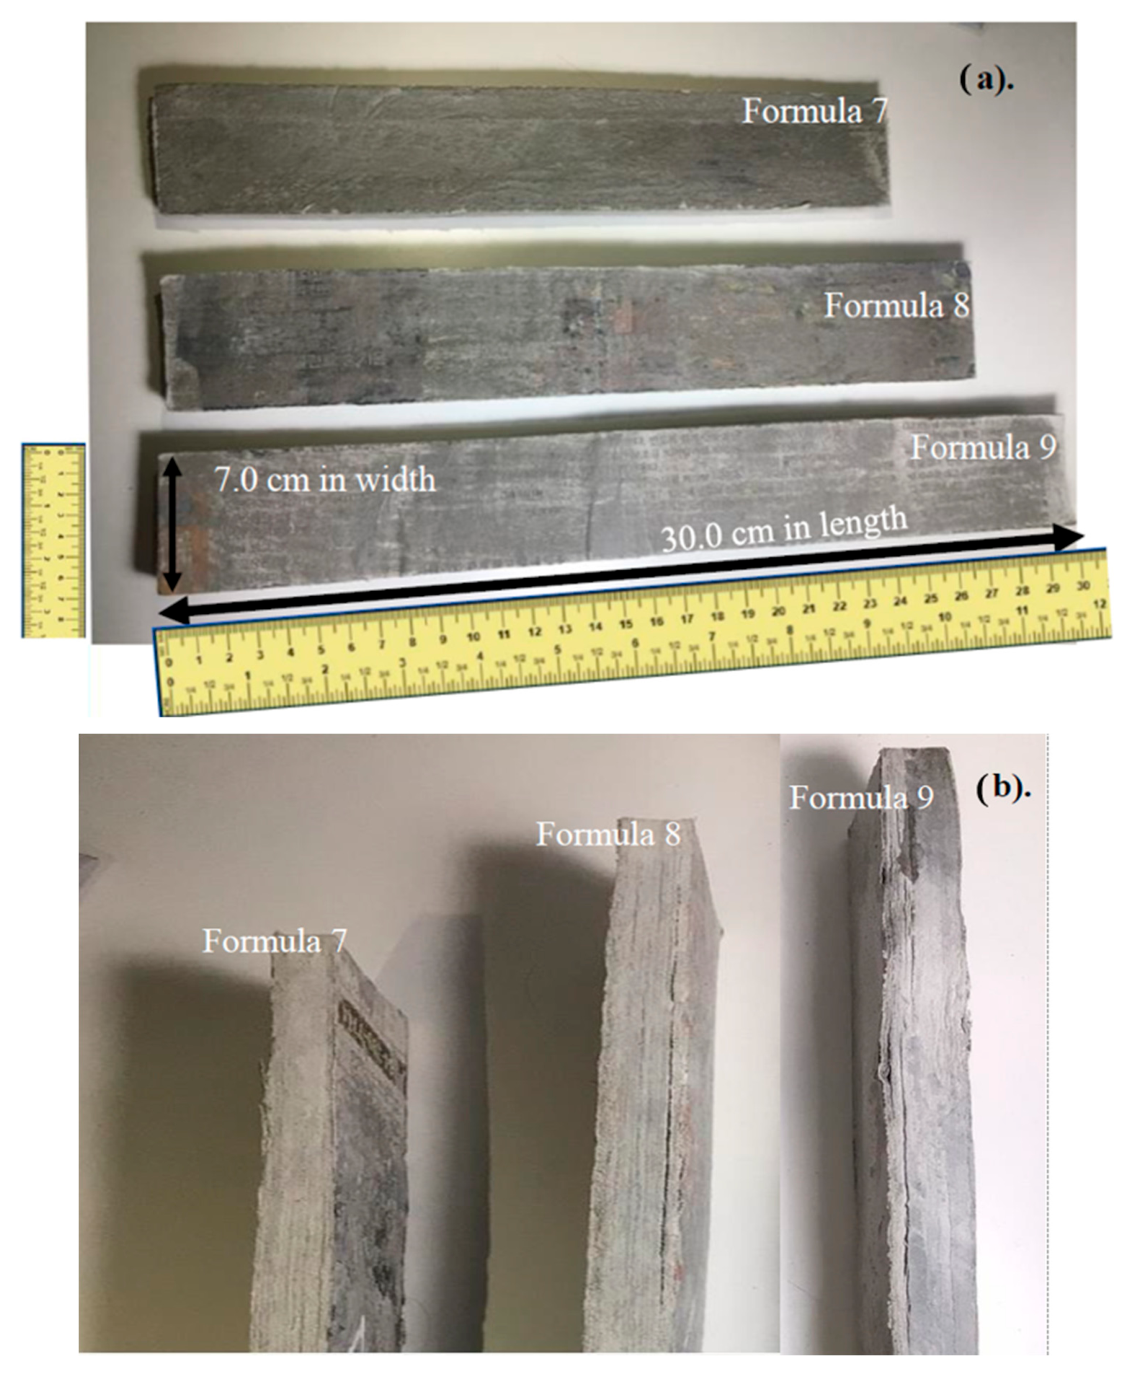
An optical microscope (OM) (modelBX51M, Olympus Corporation, Tokyo, Japan) was used to analyze the microstructure of the biofiber cement boards from specimens prepared as rectangular plates measuring 7 × 30 cm, stacked in 72, 84, and 96 layers. The microscope employed visible light and optical lenses to generate magnified images. A 10× eyepiece was used to inspect surface defects, such as cracks, shrinkage, and warping, in the prepared specimens, as shown in Figure 5 and Figure 6.
Figure 5.
Biofiber cement boards after UTM testing: (a) longitudinal sections of samples (Formulas (1)–(3)); (b) transverse sections of samples (Formulas (4)–(6)); (c) longitudinal sections of samples (Formulas (7)–(9)); (d) transverse sections of samples (Formulas (7)–(9)).
Figure 6.
Dimensions and optimal biofiber cement boards after UTM testing: (a) longitudinal sections of samples (Formulas (7)–(9)) and (b) transverse sections of samples (Formulas (7)–(9)).
A Universal Testing Machine (UTM) (model H50KS, Hounsfield, Tinius Olsen, Horsham, PA, USA) was used to evaluate the mechanical properties of the biofiber cement boards, including stress–strain behavior and Young’s modulus. The tests were conducted using a 500 N load cell, with a crosshead speed of 50 mm/min and a preload of 1 N. A maximum strain limit of 25% was set as the machine control parameter.
A three-point bending test was performed in accordance with TISI 878-2023 [43] and ASTM C1185 [45] to determine flexural strength (modulus of rupture, MOR), flexural modulus (MOE), flexural stress, and flexural strain. The specimens were prepared as rectangular bars with a width of 5 cm. The span length was defined as 16 times the specimen thickness, but not less than 150 mm, with an additional allowance to ensure that both ends extended approximately 25 mm beyond the supports. The loading apparatus was capable of measuring force with a resolution of 5 N or 5% of the maximum applied load. The loading nose had a semicircular contact surface with a radius of approximately 10 mm and a length not less than the specimen width. The supports had a circular or semicircular cross-section with a radius of approximately 10 mm. Deflection was measured using a device with a resolution of at least 0.1 mm. The load was applied at the midpoint of the specimen at a constant rate, and the time to failure was controlled within 30–120 s.
For a rectangular cross-section of flexural strength (MOR):
Calculation of the flexural strain (ϵf):
Calculation of flexural modulus (MOE, Ef):
where σf, ϵf, Ef, F, L, b, d, D, m, R according to σf = modulus of rupture (MPa); ϵf = strain on the outer surface, (mm/mm); Ef = flexural modulus of elasticity (MPa); F = load at a specific point on the load–deflection curve (N); L = support span (mm); b = width of test beam (mm); d = depth/thickness of test beam (mm); D = maximum deflection at beam center (mm); m = initial slope of the load–deflection curve (N/mm); and R = radius of specimen (mm).
Thermal conductivity was measured using a heat flow meter (HFM 446 Lambda, NETZSCH-Gerätebau GmbH, Selb, Germany) in accordance with ASTM C518. The specimens were prepared as flat plates with dimensions of 200 mm × 200 mm and a thickness of xx mm. The surfaces were made smooth and parallel to ensure proper contact with the hot and cold plates. All measurements were conducted under steady-state conditions. The tests were performed over a temperature range of 20–50 °C, with the upper plate maintained at a lower temperature than the lower plate. Thermal conductivity was calculated based on Fourier’s law using the measured heat flow through the specimen.
where K = thermal conductivity (W/m.K); Q = steady-state heat flux through the specimen (W); L = thickness of the specimen (m); A = cross-sectional area of the specimen (m2); and ΔT = temperature difference between the hot and cold plates (K or °C).
Water absorption and its effects on swelling or shrinkage were evaluated at room temperature (27 °C) according to ASTM D570 and ASTM D5890-11. Water absorption was calculated using
where is the initial dry weight, and is the weight after 24 h immersion.
Specimens were cut using a silicon carbide saw or equivalent equipment. Rectangular samples with parallel sides perpendicular to the forming surface were prepared, with a minimum volume of 25 cm3. Loose particles were removed using compressed air. Mass was recorded to an accuracy of ±0.05 g using a weighing scale with ±0.01% precision. Samples were immersed in water at (20 ± 2) °C for at least 24 h. Successive mass readings at 2 h intervals were taken until variation was below 0.5%. After immersion, surface moisture was wiped off, and the saturated mass was recorded. Specimens were then oven-dried at (105 ± 5) °C using a forced-circulation oven until consecutive mass readings at 2 h intervals showed a decrease below 0.5%. Samples were cooled in a desiccator to ambient temperature, and dry mass was recorded.
2.3. Preparation of Multilayer Structural Composite Prototypes of Biofiber Cement Boards
The characteristics of the raw materials used to produce the biofiber cement boards are presented in Table 2. Prototype biofiber cement blocks, illustrated in Figure 4, were fabricated using cement packaging sheets, a water-based adhesive, and Portland cement. The samples were produced through casting and pressing based on the formulations listed in Table 3. The ratios of water, Portland cement, and water-based adhesive were 1:1:0, 1:1:1, and 1:1:2, respectively, combined with 72, 84, and 96 cement packaging sheets arranged in a stacked configuration, forming laminated structural composite materials. A total of nine formulations were developed and designated as Formula (x–y–z), where x denotes the number of biofiber cement packaging sheets, y represents the percentage of cement by volume, and z represents the percentage of water-based adhesive by volume. Each formulation consisted of five specimens, resulting in a total of 45 samples. The prototype samples were prepared in both bar and block shapes with uniform dimensions of 7.0 cm in width and 30.0 cm in length. The thickness of each specimen depended on the number of biofiber packaging sheets used in each formulation. The samples were fabricated by sequentially stacking the layers and applying manual pressure using hand uniaxial pressing. The placement time for each layer was controlled within 1–3 min and kept consistent across all layers. One limitation of this study is the layer-by-layer assembly of cement packaging sheets in a stacked configuration, which requires careful control to ensure uniform and orderly arrangement.
Table 2.
Characteristics of raw materials for biofiber cement board production.
Table 3.
Sample preparation (mean ± standard deviation, n = 5).
This approach provides a sustainable solution for recycling construction waste and developing high-performance lightweight building materials [46,47]. The resulting composites were comprehensively characterized. Physical properties, including appearance, bulk density, water absorption, and dimensions, were evaluated using non-destructive testing (NDT). Surface appearance was assessed by visual inspection, dimensions were measured using a vernier caliper, and water absorption was determined through immersion testing. Additional physical characterization was performed using optical microscopy (OM) and quantitative analysis. Mechanical properties, including tensile strength, Young’s modulus, and bending strength, were evaluated using a Universal Testing Machine (UTM) under a three-point bending configuration. Thermal conductivity was measured using a heat flow method. An overview of the test methods for physical, mechanical, and thermal properties, all conducted in accordance with relevant standard procedures, is provided in Table 4. All experimental results are reported in this study.
Table 4.
Characterization of biofiber cement boards.
The combination of cement and biofiber sheets accelerates curing through an exothermic thermochemical reaction. Curing involves retaining sufficient moisture in the cement within an appropriate temperature range to promote hydration during the early stages. Hydration is the chemical reaction between water and cement that produces compounds responsible for the setting and hardening of the material. During curing, the heat released by the exothermic reaction also accelerates the curing of the water-based adhesive, thereby enhancing the strength and toughness of the biofiber cement boards. Formulations with higher adhesive content demonstrated improved bonding strength due to increased ionic chemical bonds and covalent interactions between the adhesive and cement layers compared to those containing little or no adhesive.
3. Results and Discussion
3.1. Characteristics and Physical Properties of Biofiber Cement Boards
The physical properties of the biofiber cement boards—including appearance, dimensions, thickness, bulk density, and water absorption percentage—were evaluated using the standard methods listed in Table 4, and the bulk density results are presented in Table 5. Visual observation of the physical characteristics of the specimens was conducted using non-destructive testing (NDT), while defects were examined using an optical microscope, as shown in Figure 5 and Figure 6.
Table 5.
Measurement of the bulk density of the biofiber cement boards.
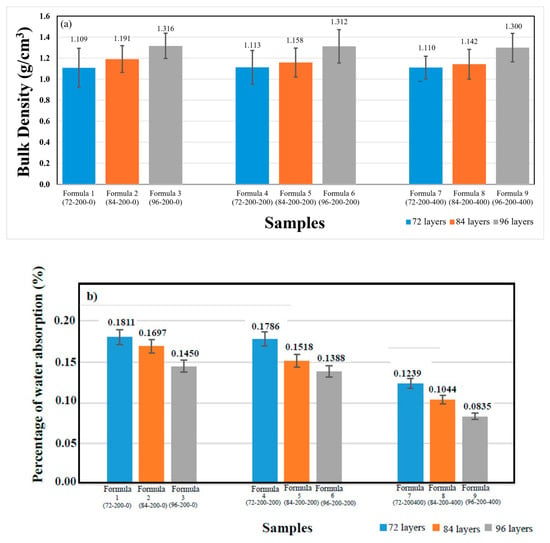
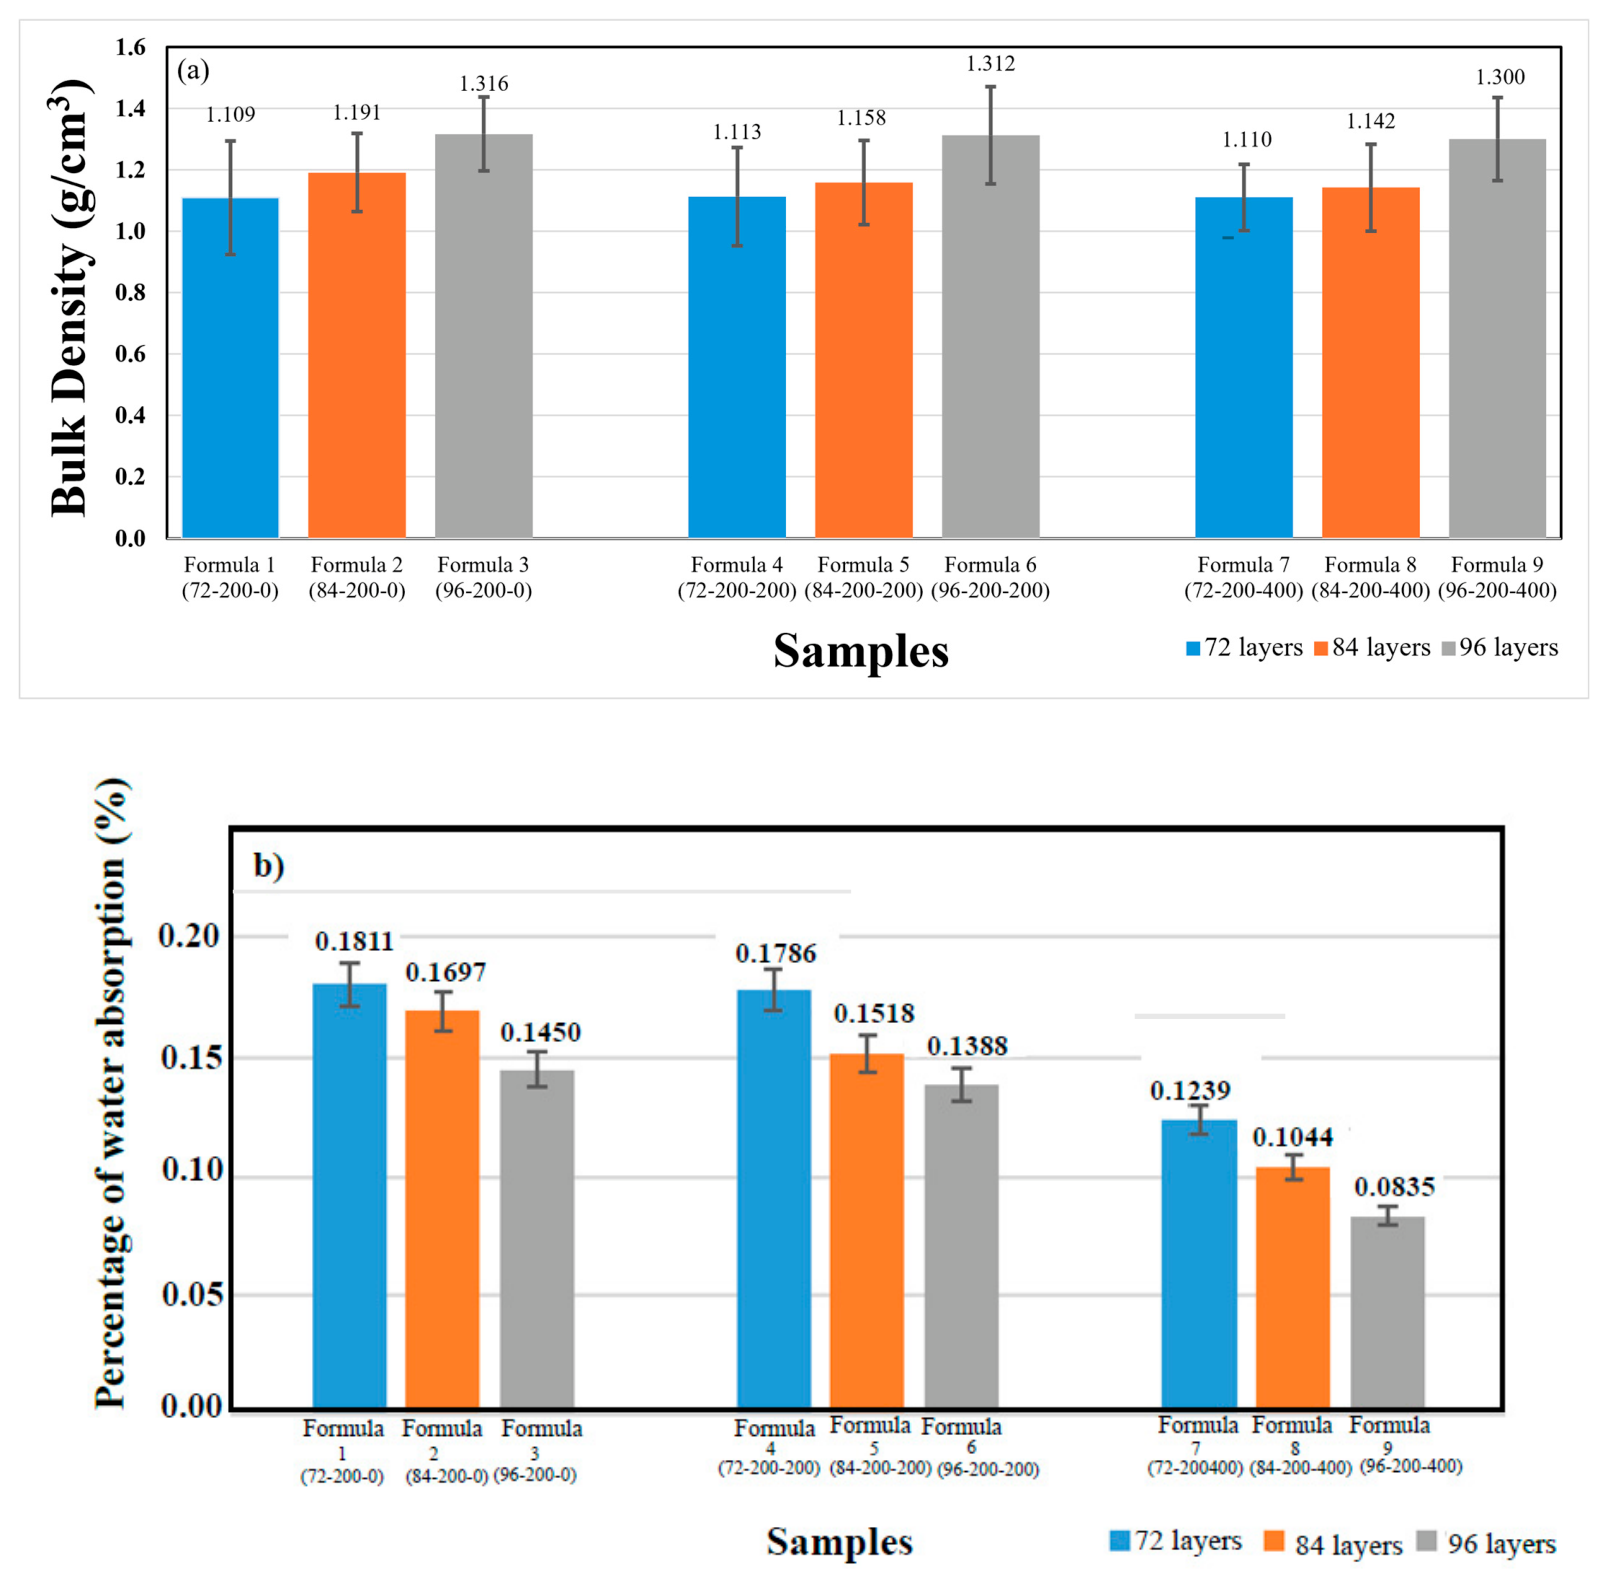
The ratio of Portland cement to water-based adhesive significantly affected the appearance, dimensions, and thickness of both the longitudinal and transverse sections of the samples. Among all samples, Formulas (7)–(9) demonstrated the most desirable appearance and physical properties (in terms of bulk density and water absorption), with no signs of warping or shrinkage. As the number of cement packaging sheets increased, the bulk density also increased. However, when the number of cement packaging sheets was held constant, increasing the ratio of Portland cement to water-based PVAc adhesive resulted in a decrease in bulk density, as shown in Table 5 and Figure 7a. This behavior occurs because the water content in the PVAc adhesive participates in cement hydration, while the hydroxyl groups in PVAc chemically and physically interact with hydration products such as C–S–H and Ca(OH)2. Additionally, PVAc chains form a polymer–cement composite network, which lowers bulk density while simultaneously enhancing chemical bonding, mechanical strength, and durability. Formulas (7)–(9) exhibited the lowest bulk densities, measured at 1.034 ± 0.108, 1.090 ± 0.120, and 1.300 ± 0.135 g/cm3, respectively. These values fall within the standard bulk density range for building materials, as illustrated in Table 1. All observed physical characteristics and performance values comply with industrial standards TISI 878:2023 [43] and BS EN 196-1:2016 [44], as summarized in Table 6 and Table 7. Water absorption percentage also decreased progressively, with Formulas (7)–(9) showing particularly low values of 0.1239 ± 0.0202%, 0.1044 ± 0.0200%, and 0.0835 ± 0.0102%, respectively. These formulations displayed smooth surfaces with no visible warping or shrinkage.
Figure 7.
Physical properties of biofiber cement boards: (a) bulk density and (b) water absorption percentage.
Table 6.
Industrial standards TISI No. 878:2023 and BS 874.
Table 7.
Physical properties and water absorption of biofiber cement boards.
All observed physical characteristics and performance values comply with industrial standards TISI 878:2023 and BS EN 196-1:2016, as summarized in Table 6.
3.2. Mechanical and Thermal Properties of Biofiber Cement Boards
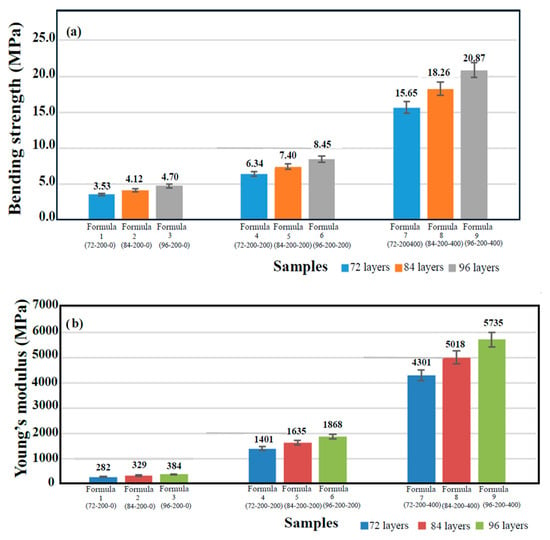
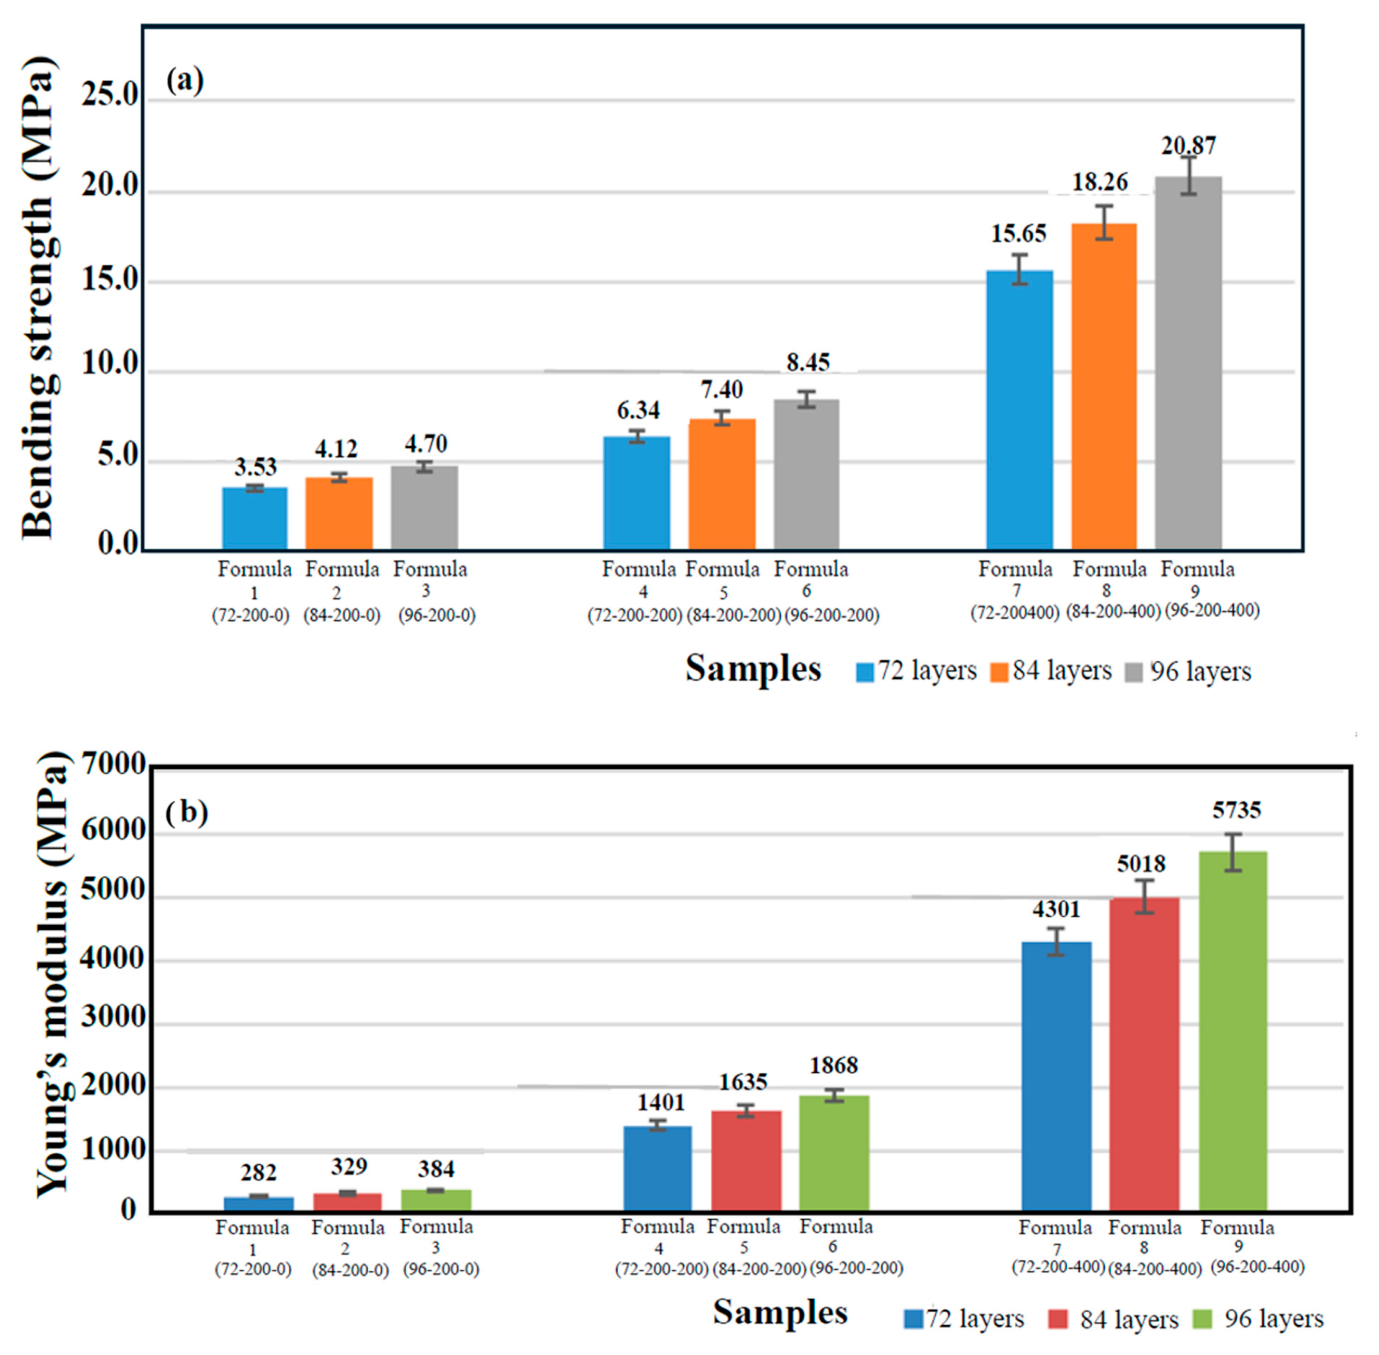
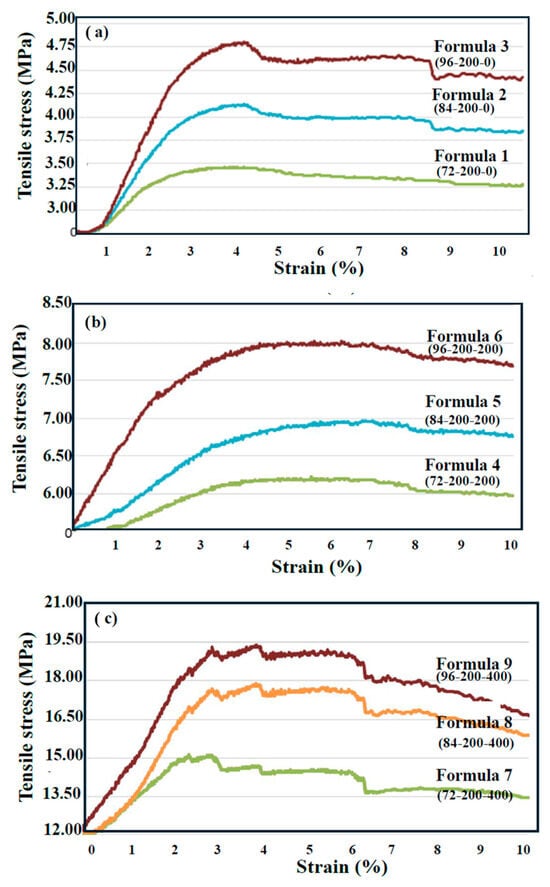
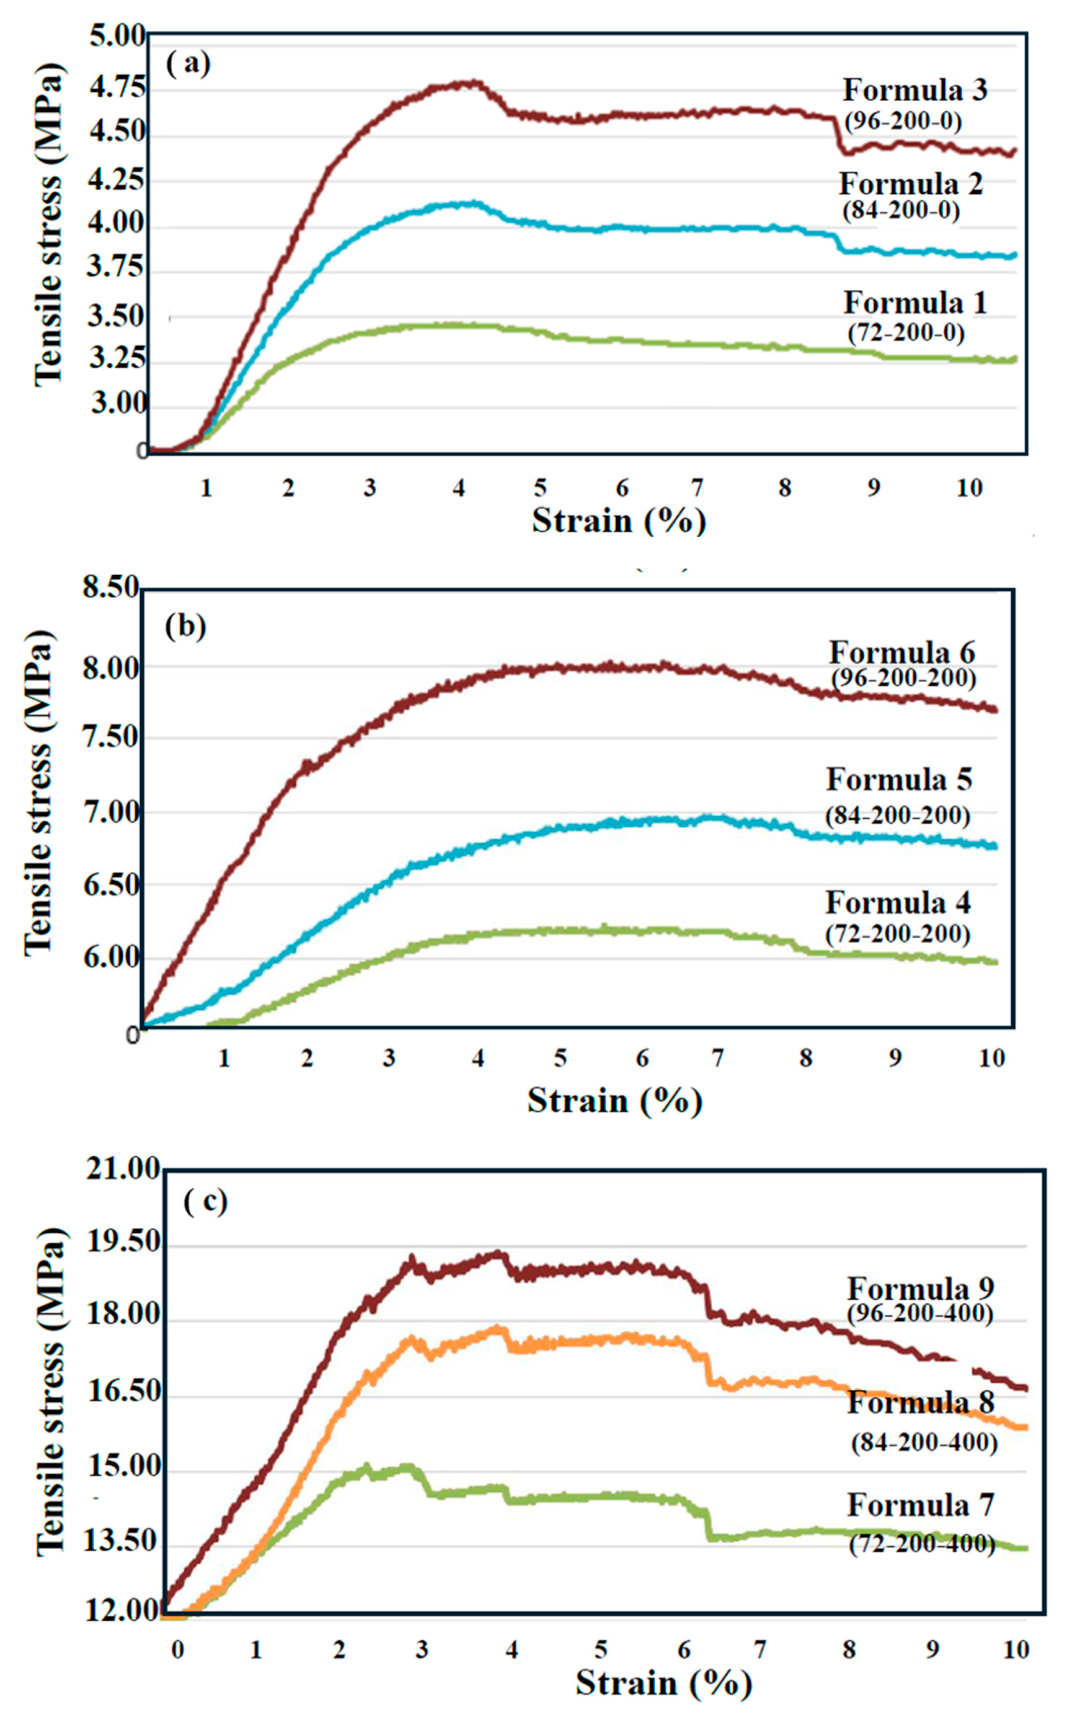
The mechanical properties, including bending strength, Young’s modulus, and tensile strength, were measured and are summarized in Table 8 and Figure 8 and Figure 9. The results show a consistent upward trend across all three properties. As the ratio of Portland cement to water-based adhesive increased from 1:0 to 1:1 to 1:2, tensile strength, bending strength, and Young’s modulus also increased proportionally. Additionally, increasing the number of biofiber cement packaging sheets further contributed to the improvement of these properties, as shown in Table 8. Among all compositions, Formulas (7)–(9) exhibited the highest performance, with tensile strengths of 15.085 ± 0.560, 17.890 ± 0.350, and 19.489 ± 0.670 MPa, bending strengths of 15.650 ± 2.609, 18.258 ± 2.555, and 20.867 ± 2.505 MPa, and moduli of elasticity of 4301.500 ± 185.650, 5018.000 ± 211.230, and 5735.068 ± 387.032 MPa, respectively (Figure 9). These results indicate that incorporating cement together with a small proportion of water-based PVAc adhesive into laminated recycled cement packaging sheets produces composites with high compressive and tensile strength suitable for industrial and construction applications. When comparing the mechanical properties of biofiber cement board composites derived from recycled cement packaging bags with the addition of a water-based adhesive at a Portland cement to water-based PVAc adhesive ratio of 1:2, the tensile and bending strengths are approximately 4–10 times higher than those of conventional materials such as cement, glass, mortar, PU foam, asphalt, marble, plasterboard, brick, red brick, and concrete, as shown in Table 1. In addition, the thermal conductivity of the prepared samples is approximately 3–10 times lower than that of other conventional insulating materials.
Table 8.
Mechanical and thermal properties of biofiber cement boards.
Figure 8.
Mechanical properties of biofiber cement boards: (a) bending strength and (b) Young’s modulus.
Figure 9.
Rela. onship between tensile stress and strain of biofiber cement boards: (a) Formulas (1)–(3); (b) Formulas (4)–(6); and (c) Formulas (7)–(9).
During cement hydration, water reacts with cement in an exothermic process that leads to hardening. The addition of PVAc improves workability and adhesion by interacting with cement while simultaneously adhering to the recycled cement packaging fibers. During curing, the PVAc polymer forms a film that bonds with the cement matrix, reinforcing the microstructure and enhancing internal cohesion. As a result, the mechanical performance of the biofiber cement boards is significantly improved. These findings are consistent with previous studies: Wong et al. reported improved mechanical strength after incorporating burnt newspaper ash particles into cement [47]. They found that the average peak compressive strength of the optimally treated concrete cylinders reached 40.39 MPa and 44.06 MPa, representing increases of 1.74% and 7.75% compared to the control specimens at curing ages of 56 and 90 days, respectively. This improvement is further supported by the low average water absorption values of 2.77% and 2.01% for the optimally treated samples at 56 and 90 days, respectively. In addition, Rajput et al. produced building materials from recycled paper mill waste with 10 wt% Portland cement [9]. They reported that bricks containing 1–5% CW and 10% cement in PCW exhibited compressive strengths in the range of 21–23 MPa (with approximately 30% shrinkage), which are significantly higher than those of conventional clay bricks and meet the requirements for indoor structural applications. Notably, these bricks undergo gradual deformation under pressure without exhibiting sudden brittle failure. Similarly, Sales et al. demonstrated that fiberboard panels produced from reclaimed paper bags (both fiber and pulp forms) and bonded with urea–formaldehyde thermosetting resin exhibited improved flexural strength and elastic modulus [46]. They concluded that discarded cement bags made of Kraft paper are a promising material for indoor construction applications. The flexural performance, evaluated in terms of modulus of elasticity (MOE) and modulus of rupture (MOR), showed strong results, with mean values of 465.5 N/mm2 (MOE) and 16.3 N/mm2 (MOR) for 15% urea–formaldehyde resin and 1299.8 N/mm2 (MOE) and 24.9 N/mm2 (MOR) for 30% urea–formaldehyde resin. Furthermore, Ardanuy et al. confirmed that cellulose fiber reinforcement enhances the mechanical, physical, and durability properties of cement composites [18]. They noted that cellulose cement composites are typically manufactured as thin panels, for which the most appropriate mechanical testing method is the four-point bending configuration. Significant advancements in mechanical performance and durability have been achieved over the past decade. However, future challenges remain in further improving these properties without increasing production costs, while also promoting environmentally friendly technologies.
Thermal properties were evaluated using a heat flow meter for samples corresponding to Formulas (7)–(9), as listed in Table 8. The thermal conductivity values were 0.149, 0.150, and 0.152 W/m·K, respectively, which fall within the acceptable range for cement-bonded particleboards specified in TISI 878:2023 and BS EN 196-1:2016 standards (<0.155 W/m·K; Table 6). The recycled biofiber sheets act as cellulose-based reinforcement that introduces air-filled pores, which reduce thermal conductivity due to the insulating nature of air. The PVAc film stabilizes these pores, preventing collapse during curing and resulting in a lightweight structure with enhanced thermal insulation. Typically, cement alone has a relatively high thermal conductivity (~1.01 W/m·K), whereas PVAc has a much lower value (~0.18 W/m·K). Therefore, incorporating PVAc into the cement matrix decreases the effective thermal conductivity, improving resistance to heat transfer. Furthermore, while cement hydration releases heat, PVAc partially coats cement grains, slowing hydration and moderating heat release, thus reducing the risk of thermal cracking. In addition, PVAc forms bonds with Ca2+ ions and hydrogen bonds with cellulose fibers from the biofiber cement sheets, creating a polymer–fiber–cement network that retains moisture and buffers temperature fluctuations. Although PVAc is organic, it becomes encapsulated within the cement matrix. Cement is inherently fire-resistant, and the PVAc–cellulose network promotes char formation, which acts as a thermal barrier, slowing heat penetration and improving fire resistance. Table 9 summarizes the tests conducted on each biofiber cement board specimen prepared in this study. These tests were carried out to compare the mechanical, thermal, and physical properties of the biofiber cement boards with relevant standard requirements, including bulk density, bending strength, Young’s modulus, tensile strength, water absorption, and thermal conductivity. Overall, formulations 7, 8, and 9 exhibited the most favorable performance and met the standard criteria for biofiber cement boards and related building materials.
Table 9.
Summary of the tests performed on each specimen prepared in this study.
4. Conclusions
Biofiber cement boards were successfully fabricated as structural composite materials. The cement packaging biofiber sheets functioned as the reinforcing phase, while Portland cement and water-based PVAc adhesive served as the matrix phase. Increasing the number of biofiber sheets led to improvements in the physical, mechanical, and thermal properties of the boards. Additionally, higher ratios of Portland cement to water-based adhesive further enhanced these properties. The most suitable formulations identified in this study were Formulas (7)–(9), which exhibited the following performance ranges:
- Tensile Strength: 15.085 ± 0.560, 17.890 ± 0.350, and 19.489 ± 0.670 MPa, respectively;
- Bending Strength: 15.650 ± 2.609, 18.258 ± 2.555, and 20.867 ± 2.505 MPa, respectively;
- Modulus of Elasticity: 4301.500 ± 185.650, 5018.000 ± 211.230, and 5735.068 ± 387.032 MPa, respectively.
All physical, mechanical, and thermal properties measured were consistent with and fell within the standard limits specified by ASTM D570, ASTM D5890-11, ASTM C518, ISO 8301, ASTM C1185, and JIS A1412. The thermal conductivity values of Formulas (7), (8), and (9)—0.149, 0.150, and 0.152 W/m·K, respectively—also meet the criteria for insulation materials suitable for decorative applications, ceiling panels, and wall construction. The addition of a water-based PVAc adhesive improves tensile strength, flexural strength, and heat resistance, while also reducing water absorption. This improvement is attributed to the ability of the water-based PVAc adhesive to enhance the curing rate and strengthen the interfacial bonding within the biofiber cement board. Furthermore, the mechanical strength of the biofiber cement board samples was approximately 4–10 times higher than that of the reference formulation with the lowest Portland cement-to-water-based adhesive ratio (1:0).
Author Contributions
Conceptualization, N.T.; Methodology, P.P.; Formal analysis, P.P. and N.T.; Investigation, P.P.; Resources, P.P. and N.T.; Data curation, N.T.; Writing—original draft, N.T.; Visualization, N.T.; Supervision, N.T.; Project administration, N.T. All authors have read and agreed to the published version of the manuscript.
Funding
The authors would like to acknowledge the financial support from the Department of Materials Engineering, Kasetsart University, for sample analysis in this research.
Data Availability Statement
The original contributions presented in this study are included in the article. Further inquiries can be directed to the corresponding author.
Acknowledgments
The authors extend their sincere gratitude to the Department of Materials Engineering, Kasetsart University, Bangkok, Thailand, for granting access to the analytical equipment essential for this research.
Conflicts of Interest
The authors declare that there are no conflicts of interest.
References
- Scrivener, K.L.; John, V.M.; Gartner, E.M. Eco-efficient cements: Potential economically viable solutions for a low-CO2 cement-based materials industry. Cem. Concr. Res. 2018, 114, 2–26. [Google Scholar] [CrossRef] [Scilit]
- Mehta, P.K.; Monteiro, P.J.M. Concrete: Microstructure, Properties, and Materials; McGraw-Hill Education: New York, NY, USA, 2014. [Google Scholar]
- Juenger, M.C.G.; Snellings, R.; Bernal, S.A. Supplementary cementitious materials: New sources, characterization, and performance insights. Cem. Concr. Res. 2019, 122, 257–273. [Google Scholar] [CrossRef] [Scilit]
- John, M.J.; Thomas, S. Biofibres and biocomposites. Carbohydr. Polym. 2008, 71, 343–364. [Google Scholar] [CrossRef] [Scilit]
- Faruk, O.; Bledzki, A.K.; Fink, H.P.; Sain, M. Biocomposites reinforced with natural fibers: 2000–2010. Prog. Polym. Sci. 2012, 37, 1552–1596. [Google Scholar] [CrossRef] [Scilit]
- Satyanarayana, K.G.; Arizaga, G.G.C.; Wypych, F. Biodegradable composites based on lignocellulosic fibers—An overview. Prog. Polym. Sci. 2009, 34, 982–1021. [Google Scholar] [CrossRef] [Scilit]
- Okada, K.; Yamamoto, N.; Kameshima, Y.; Yasumori, A. Porous properties of activated carbons from waste newspaper prepared by chemical and physical activation. J. Colloid Interface Sci. 2003, 262, 179–193. [Google Scholar] [CrossRef] [Scilit]
- Ashori, A.; Tabarsa, T.; Valizadeh, I. Fiber reinforced cement boards made from recycled newsprint paper. Mater. Sci. Eng. A 2011, 528, 7801–7804. [Google Scholar] [CrossRef] [Scilit]
- Rajput, D.; Bhagade, S.S.; Raut, S.P.; Ralegaonkar, R.V.; Mandavgane, S.A. Reuse of cotton and recycle paper mill waste as building material. Constr. Build. Mater. 2012, 34, 470–475. [Google Scholar] [CrossRef] [Scilit]
- Jensen, M.S.; Alfieri, P.V. Design and manufacture of insulation panels based on recycled lignocellulosic waste. Clean. Eng. Technol. 2021, 3, 100111. [Google Scholar] [CrossRef] [Scilit]
- Mazaherifar, M.H.; Coșereanu, C.; Timar, C.M.; Georgescu, S.V. Physical and mechanical properties of foam-type panels manufactured from recycled cardboard. Constr. Build. Mater. 2024, 411, 134685. [Google Scholar] [CrossRef] [Scilit]
- Chen, S.; Chen, Y.; Li, D.; Xu, Y.; Xu, F. Flexible and sensitivity-adjustable pressure sensors based on carbonized bacterial nanocellulose/wood-derived cellulose nanofibril composite aerogels. ACS Appl. Mater. Interfaces 2021, 13, 8754–8763. [Google Scholar] [CrossRef] [Scilit]
- Yang, C.; Wu, Q.; Xie, W.; Zhang, X.; Brozena, A.H.; Zheng, J.; Garaga, M.N.; Ko, B.H.; Mao, Y.; He, S.; et al. Copper-coordinated cellulose ion conductors for solid-state batteries. Nature 2021, 598, 590–596. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Vicente, A.T.; Araújo, A.; Mendes, M.J.; Nunes, D.; Oliveira, M.J.; Sanchez-Sobrado, O.; Ferreira, M.P.; Águas, H.; Fortunato, E.; Martins, R. Multifunctional cellulose-paper for light harvesting and smart sensing applications. J. Mater. Chem. C 2018, 6, 3143–3181. [Google Scholar] [CrossRef] [Scilit]
- Sun, Z.; Qu, K.; You, Y.; Huang, Z.; Liu, S.; Li, J.; Hu, Q.; Guo, Z. Overview of cellulose-based flexible materials for supercapacitors. J. Mater. Chem. A 2021, 9, 7278–7300. [Google Scholar] [CrossRef] [Scilit]
- Tafete, G.A.; Abera, M.K.; Thothadri, G. Review on nanocellulose-based materials for supercapacitors applications. J. Energy Storage 2022, 48, 103938. [Google Scholar] [CrossRef] [Scilit]
- Roma, L.C., Jr.; Martello, L.S.; Savastano, H., Jr. Evaluation of mechanical, physical and thermal performance of cement-based tiles reinforced with vegetable fibers. Constr. Build. Mater. 2008, 22, 668–674. [Google Scholar] [CrossRef] [Scilit]
- Ardanuy, M.; Claramunt, J.; Toledo Filho, R.D. Cellulosic fiber reinforced cement-based composites: A review of recent research. Constr. Build. Mater. 2015, 79, 115–128. [Google Scholar] [CrossRef] [Scilit]
- Wei, J.; Meyer, C. Degradation mechanisms of natural fibers in the matrix of cement composites. Cem. Concr. Res. 2015, 73, 1–16. [Google Scholar] [CrossRef] [Scilit]
- Křížová, K.; Baránek, S.; Bubenik, J.; Mazán, T. Study of the behaviour of recycled and traditional fibres in cement composite at extreme temperatures. J. Build. Eng. 2024, 95, 110134. [Google Scholar] [CrossRef] [Scilit]
- Pickering, K.L.; Efendy, M.G.A.; Le, T.M. A review of recent developments in natural fibre composites and their mechanical performance. Compos. Part A Appl. Sci. Manuf. 2016, 83, 98–112. [Google Scholar] [CrossRef] [Scilit]
- Ferreira, S.R.; Silva, F.A.; Toledo Filho, R.D. Effect of fiber treatments on the sisal fiber properties and fiber–matrix bond in cement-based systems. Constr. Build. Mater. 2015, 101, 730–740. [Google Scholar] [CrossRef] [Scilit]
- Toledo Filho, R.D.; Scrivener, K.; England, G.L.; Ghavami, K. Durability of alkali-sensitive sisal and coconut fibres in cement mortar composites. Cem. Concr. Compos. 2000, 22, 127–143. [Google Scholar] [CrossRef] [Scilit]
- Savastano, H.; Warden, P.G.; Coutts, R.S.P. Microstructure and mechanical properties of waste fibre-cement composites. Cem. Concr. Compos. 2005, 27, 583–592. [Google Scholar] [CrossRef] [Scilit]
- Mohr, B.J.; Nanko, H.; Kurtis, K.E. Durability of kraft pulp fiber–cement composites to wet/dry cycling. Cem. Concr. Compos. 2005, 27, 435–448. [Google Scholar] [CrossRef] [Scilit]
- Almeida, A.E.F.S.; Tonoli, G.H.D.; Santos, S.F.; Savastano, H., Jr. Improved durability of vegetable fiber reinforced cement composite subject to accelerated carbonation at early age. Cem. Concr. Compos. 2013, 42, 49–58. [Google Scholar] [CrossRef] [Scilit]
- Li, H.; Zhang, Y.; Liu, G.; Peng, G.; Li, Y. Polymer-modified cement mortars: Their enhanced properties, applications, prospects, and challenges. Constr. Build. Mater. 2021, 299, 124290. [Google Scholar] [CrossRef] [Scilit]
- Zhou, Y.; Kamdem, D.P. Effect of cement/wood ratio on the properties of cement-bonded particleboard using CCA-treated wood removed from service. For. Prod. J. 2002, 52, 77–81. [Google Scholar]
- Taiwo, A.S.; Ayre, D.S.; Khorami, M.; Rahatekar, S.S. Optimizing the Mechanical Properties of Cement Composite Boards Reinforced with Cellulose Pulp and Bamboo Fibers for Building Applications in Low-Cost Housing Estates. Materials 2024, 17, 646. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Diao, R.; Cao, Y.; Michel, M.M.; Wang, A.; Sun, L.; Yang, F. Mechanical performance study of PVA fiber-reinforced seawater and sea sand cement-based composite materials. Sci. Rep. 2024, 14, 18161. [Google Scholar] [CrossRef] [Scilit]
- Thong, C.C.; Teo, D.C.L.; Ng, C.K. Application of polyvinyl alcohol (PVA) in cement-based composite materials: A review of its engineering properties and microstructure behavior. Constr. Build. Mater. 2016, 107, 172–180. [Google Scholar] [CrossRef] [Scilit]
- Ali, H.; Gaël, C.; Eric, L.; Pierre, M.; Rémi, D. The kinetic behavior of liquid silicone rubber: A comparison between thermal and rheological approaches. React. Funct. Polym. 2016, 101, 20–27. [Google Scholar] [CrossRef] [Scilit]
- Hong, I.-K.; Lee, S. Cure kinetics and modeling the reaction of silicone rubber. J. Ind. Eng. Chem. 2013, 19, 42–47. [Google Scholar] [CrossRef] [Scilit]
- Oktay, S.; Pizzi, A.; Koken, N.; Bengü, B. Chemical modification techniques of corn starch for synthesis wood adhesive. Int. J. Adhes. Adhes. 2024, 128, 103545. [Google Scholar] [CrossRef] [Scilit]
- Xu, Y.; Zhang, Q.; Lei, H.; Zhou, X.; Zhao, D.; Du, G.; Pizzi, A.; Xi, X. A formaldehyde-free amino resin alternative to urea-formaldehyde adhesives: A bio-based oxidized glucose—urea resin. Ind. Crops Prod. 2024, 218, 119037. [Google Scholar] [CrossRef] [Scilit]
- Hussin, M.H.; Latif, N.H.A.; Hamidon, T.S.; Idris, N.N.; Hashim, R.; Appaturi, J.N.; Brosse, N.; Ziegler-Devin, I.; Chrusiel, L.; Fatriasari, W.; et al. Latest advancements in high-performance bio-based wood adhesives. J. Mater. Res. Technol. 2022, 21, 3909–3946. [Google Scholar] [CrossRef] [Scilit]
- Lim, M.; Kwon, H.; Kim, J.; Seo, J.; Han, H.; Khan, S.B. Highly enhanced water resistant and oxygen barrier properties of cross-linked poly(vinyl alcohol) hybrid films. Prog. Org. Coat. 2015, 85, 68–75. [Google Scholar] [CrossRef] [Scilit]
- Krenchel, H. Fibre Reinforcement: Theoretical and Practical Investigations; Akademisk Forlag: Copenhagen, Denmark, 1964. [Google Scholar]
- Cox, H.L. The elasticity and strength of paper and other fibrous materials. Br. J. Appl. Phys. 1952, 3, 72–79. [Google Scholar] [CrossRef] [Scilit]
- Booya, E.; Gorospe, K.; Ghaednia, H.; Das, S. Durability properties of engineered pulp fibre reinforced concretes made with and without supplementary cementitious materials. Compos. Part B Eng. 2019, 172, 376–386. [Google Scholar] [CrossRef] [Scilit]
- Neithalath, N.; Weiss, J.; Olek, J. Acoustic performance and damping behavior of cellulose-cement composites. Cem. Concr. Compos. 2004, 26, 359–370. [Google Scholar] [CrossRef] [Scilit]
- Gomez, T.S.; Zuluaga, S.; Jimenez, M.; de la Prida, D.; Pedrero, A.; Navacerrada, M.Á.; Restrepo-Osorio, A.; Fernandez-Morales, P. Sound absorption behavior of repurposed waste fibers: Effects of fiber size, density, and binder concentration. Appl. Acoust. 2023, 202, 109174. [Google Scholar] [CrossRef] [Scilit]
- TISI 878-2023; Portland Cement—Specification. Thai Industrial Standards Institute (TISI): Bangkok, Thailand, 2023.
- BS EN 196-1:2016; Methods of Testing Cement—Part 1: Determination of Strength. BSI: London, UK, 2016.
- ASTM C1185; Standard Test Methods for Sampling and Testing Non-Asbestos Fiber-Cement Flat Sheet, Roofing and Siding Shingles, and Clapboards. ASTM International: West Conshohocken, PA, USA, 2019.
- Sales, D.C.; Cabral, A.E.; Medeiros, M.S. Development of fiberboard panels manufactured from reclaimed cement bags. J. Build. Eng. 2021, 34, 101525. [Google Scholar] [CrossRef] [Scilit]
- Wong, L.S.; Chandran, S.N.; Rajasekar, R.R.; Kong, S.Y. Pozzolanic characterization of waste newspaper ash as a supplementary cementing material. Case Stud. Constr. Mater. 2022, 17, e01342. [Google Scholar] [CrossRef] [Scilit]
- ASTM D570; Standard Test Method for Water Absorption of Plastics. ASTM International: West Conshohocken, PA, USA, 2018.
- ASTM D5890-11; Standard Test Method for Swelling Index of Coal. ASTM International: West Conshohocken, PA, USA, 2011.
- ASTM C518; Standard Test Method for Steady-State Thermal Transmission Properties by Means of the Heat Flow Meter Apparatus. ASTM International: West Conshohocken, PA, USA, 2021.
- ISO 8301; Thermal Insulation—Determination of Steady-State Thermal Resistance and Related Properties—Heat Flow Meter Apparatus. International Organization for Standardization (ISO): Geneva, Switzerland, 2018.
- JIS A1412; Thermal Insulation—Measurement of Thermal Resistance by the Heat Flow Meter Method. Japanese Standards Association (JSA): Tokyo, Japan, 2015.

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.