


Abstract
Binder jetting additive manufacturing (BJAM) offers an effective approach for fabricating silicon carbide (SiC) parts with complex geometries; however, part quality is strongly influenced by process variables. Binder saturation and drying time are key process variables in BJAM, yet their individual influences on the density and dimensional deviation of SiC green parts remain underexplored. To address this gap, this study systematically investigates the effects of binder saturation and drying time on the dimensional deviation and density of SiC green parts by evaluating four binder saturation levels (60%, 80%, 100%, and 120%) and three drying times (15, 30, and 45 s). The results show that increasing binder saturation reduces green part density and increases dimensional deviation, whereas increasing drying time improves density and reduces dimensional deviation. Excessive drying, however, causes severe warpage, preventing the fabrication of dimensionally accurate parts. These findings highlight the need to optimize binder saturation and drying time to improve the density of printed parts while minimizing dimensional deviation.
1. Introduction
Silicon carbide (SiC) exhibits a combination of exceptional characteristics [1], including high hardness, excellent thermal conductivity, chemical stability, and strong resistance to wear and corrosion [2]. Because of these attributes, SiC is widely employed in high-performance applications across the aerospace, automotive, and energy sectors, where materials must function reliably under extreme environmental and mechanical conditions [3,4,5,6]. Despite these advantages, the same properties that make SiC valuable also make it difficult to manufacture using traditional techniques. Conventional fabrication approaches—such as hot pressing, sintering, and infiltration—typically require very high temperatures and substantial energy consumption, leading to long processing cycles and increased production costs. Furthermore, producing SiC parts with complex geometries using these methods is challenging without specialized tooling or extensive post-processing.
Binder jetting additive manufacturing (BJAM) offers an alternative for producing SiC components [7,8,9]. BJAM fabricates parts layer by layer by depositing a liquid binder onto selected regions of a powder bed. These printed parts typically require subsequent post-processing—such as sintering—to achieve their final form and properties. BJAM can be used to fabricate customized ceramic components with complex shapes [10].
The quality (density and dimensional deviation) of green parts produced by BJAM is influenced by several process variables (including binder saturation and drying time). Here, green parts refer to the printed parts after printing and curing but before other post-printing steps (such as debinding and sintering). Debinding removes the binder from green parts by heating, and sintering at high temperature fuses powder particles together, increasing the strength and density of the parts. After sintering, green parts are referred to as sintered parts.
Binder saturation in BJAM refers to the percentage of void space between powder particles that is filled with liquid binder. It affects particle bonding and green part strength [11]. Drying time in BJAM refers to the time when a heat lamp passes over the powder bed for each layer to remove moisture and solidify the binder [12].
Table 1 shows reported studies regarding the effects of binder saturation and drying time on parts in binder jetting. Reported studies have investigated the effects of binder saturation in binder jetting additive manufacturing (BJAM) on density [13,14,15,16], dimensional deviation [12,17,18,19], and strength [12,15,18,19,20] of green and sintered parts. With respect to density, reported studies have primarily focused on sintered or post-processed parts, with only a limited number of studies explicitly evaluating green parts [12,15,16]. For example, Mostafaei et al. investigated the effects of binder saturation on green part density using a WC–Co composite but did not investigate the dimensional deviation of the green parts [15]. Huang et al. examined the effects of binder saturation on both density and dimensional deviation of green parts, but the study was conducted using ZrO2 powder with relatively low binder saturation levels from 7 to 17% [16]. Miyanaji et al. focused exclusively on the effects of binder saturation on the dimensional deviation of green parts using porcelain and reported experimental results at only two levels of binder saturation [12]. No reported studies have investigated the effects of binder saturation (with a wide range) on both density and dimensional deviation of green parts using SiC powder.
Table 1.
Relevant reported studies regarding the effects of binder saturation and drying time in binder jetting.
The effects of drying time in BJAM have been examined in reported studies under very limited experimental conditions [12,15]. For example, Mostafaei et al. investigated the effects of drying time on green part density for a WC–Co composite using only two levels of drying time and did not examine the effects on dimensional deviation of green parts [15]. Because a two-level design captures only linear trends, it cannot reveal potential nonlinear trends. Miyanaji et al. investigated the effects of drying time on the dimensional deviation of green parts using porcelain and did not report the effects on the density of green parts [12]. As a result, there are no reported studies on the effects of drying time on the density and dimensional deviation of green parts for SiC powder over a wider range of drying time.
As summarized in Table 1, no reported studies have specifically examined the effects of binder saturation and drying time in binder jetting of silicon carbide (SiC) powder. It is uncertain whether trends reported for metals, polymer-based, and other ceramic powders can be applied to SiC powder [1,21]. Therefore, this paper fills a gap by reporting a systematic investigation of the effects of binder saturation and drying time on dimensional deviation and density of SiC green parts in BJAM. The organization of this paper is as follows: The introduction is presented first, followed by Section 2, which describes the materials and methods employed in the study. Section 3 presents the effects of binder saturation and drying time on dimensional deviation and density of green parts. Lastly, Section 4 presents the conclusions drawn from this study.
2. Experimental Method
2.1. Feedstock Material
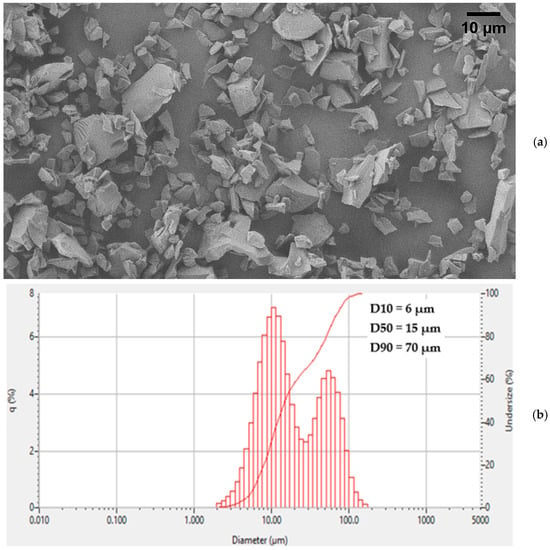
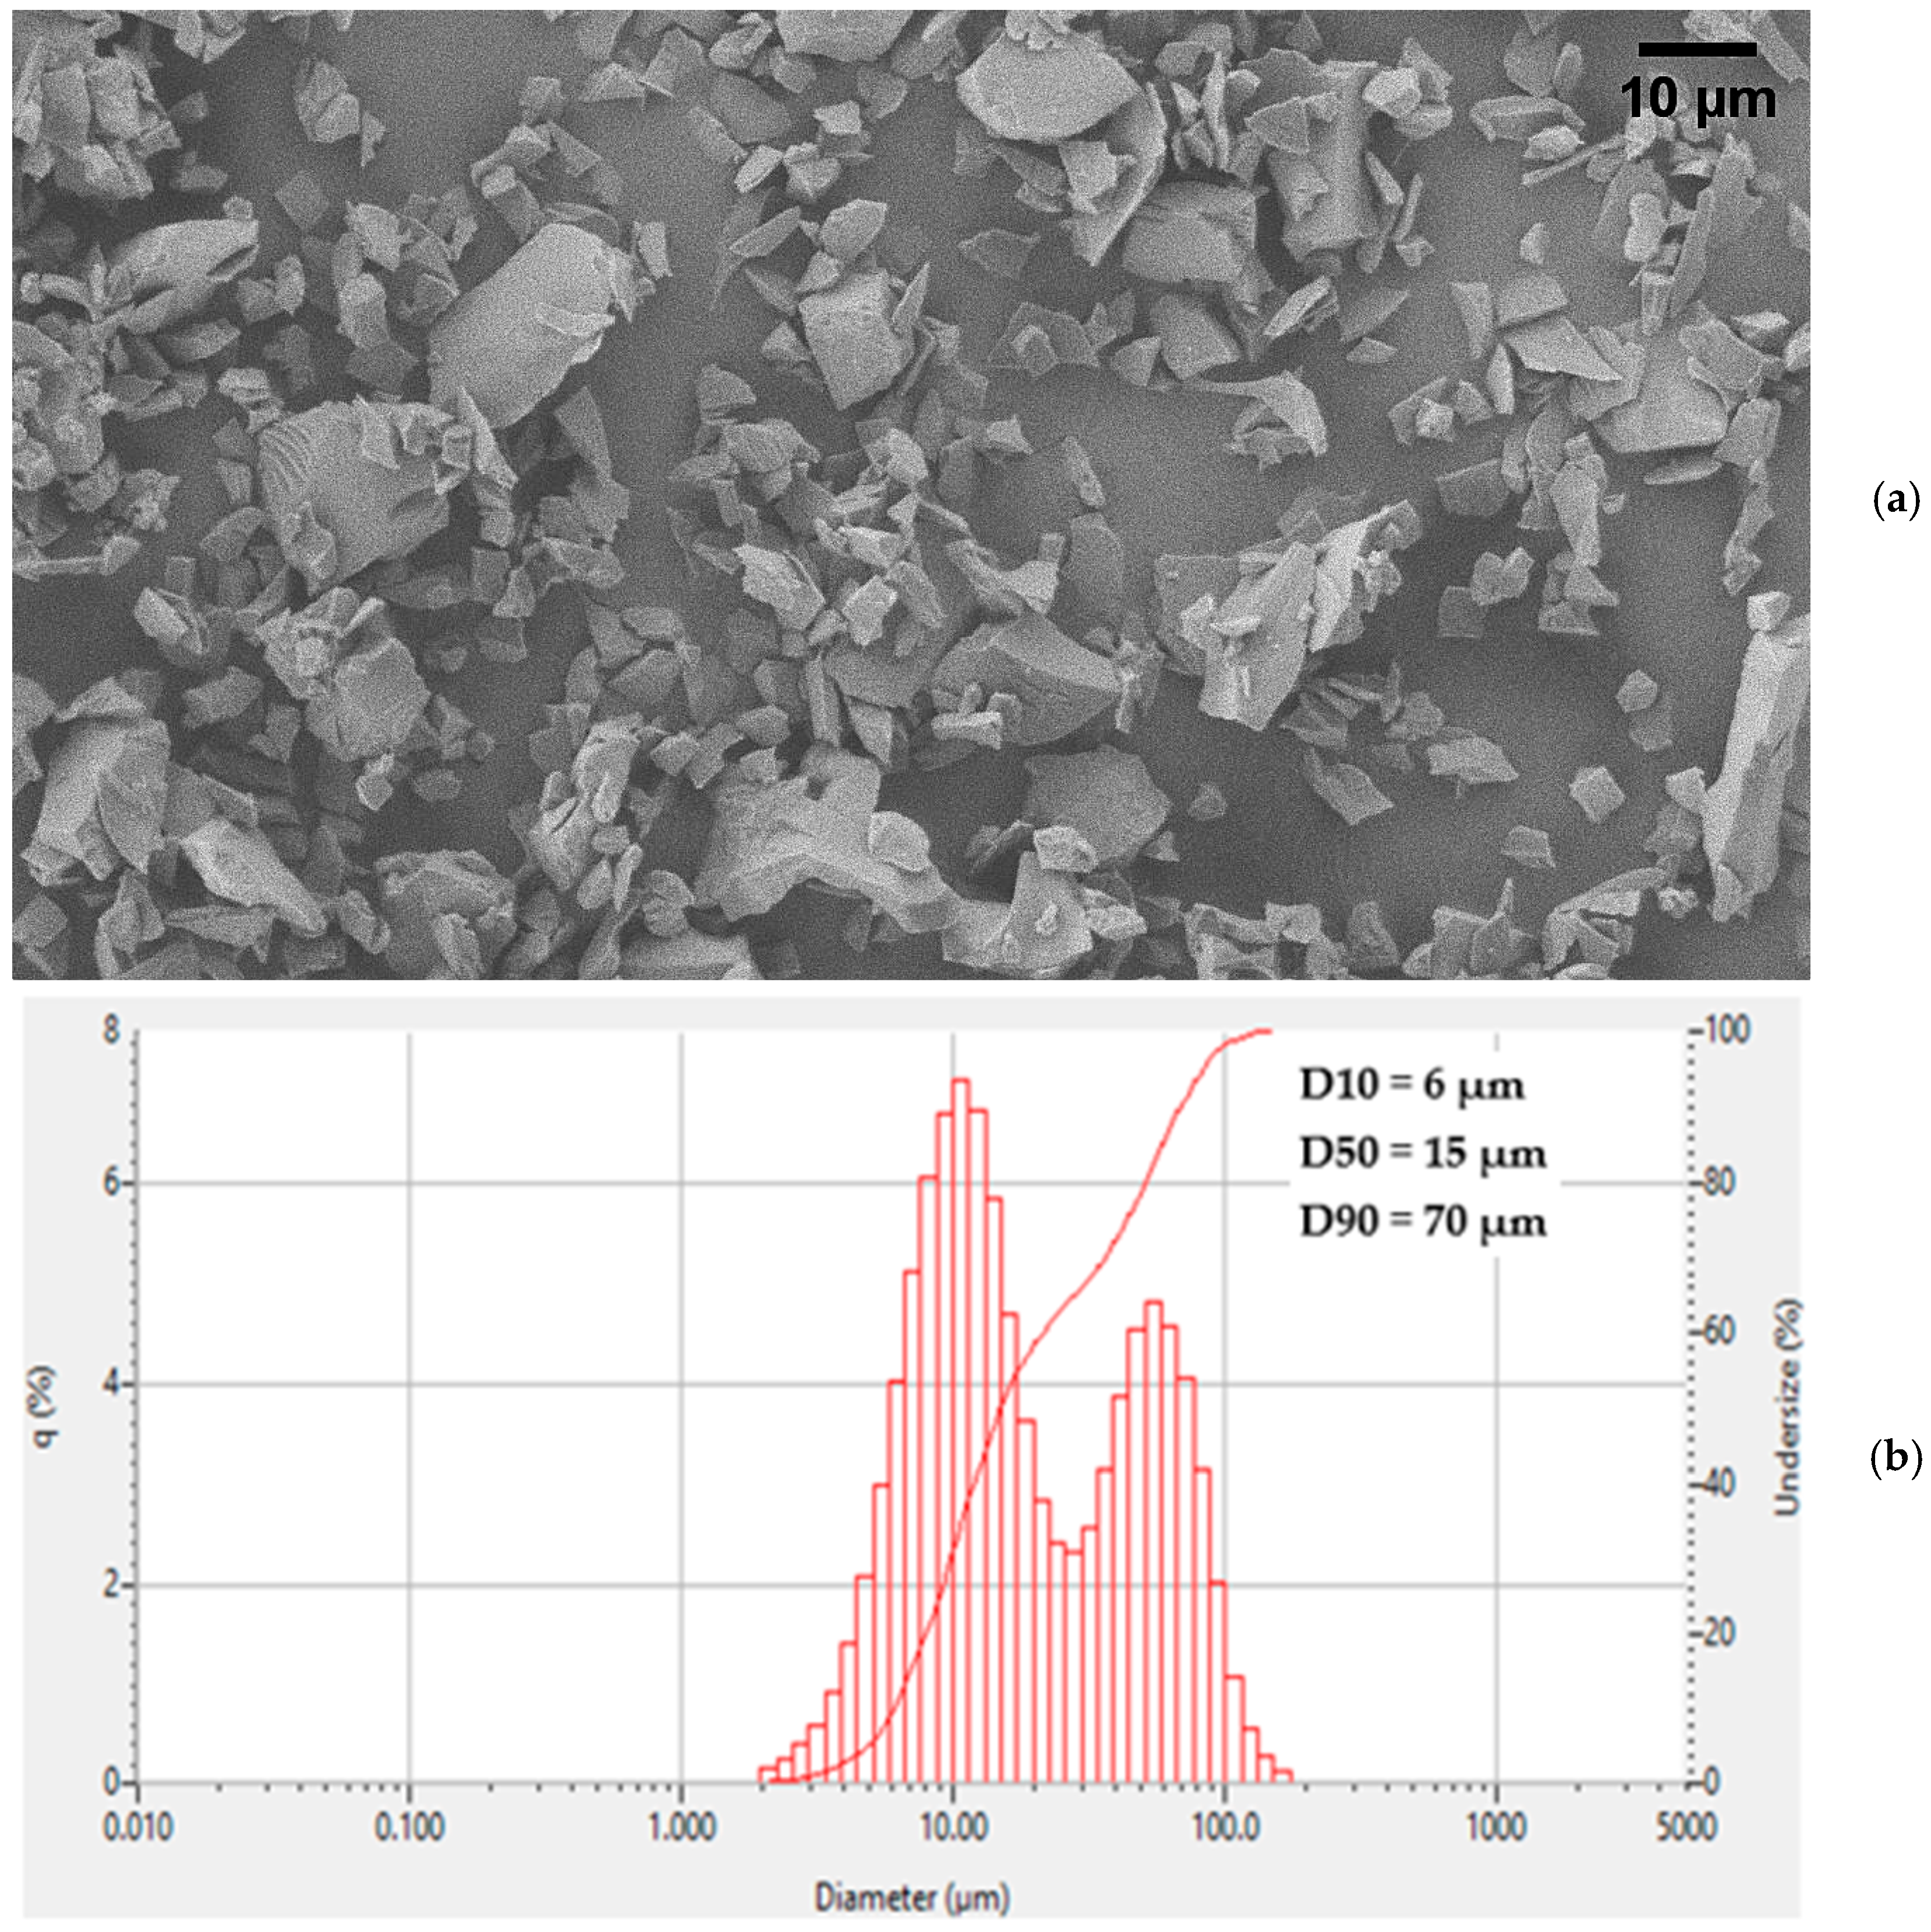
The silicon carbide (SiC) powder used in this study was supplied by Electro Abrasives LLC (Buffalo, NY, USA). A laser scattering particle size analyzer (Horiba LA-960, Kyoto, Japan) was used to measure the particle size distribution (PSD) of as-received SiC powder. The PSD results showed D10, D50, and D90 values of 6 μm, 14 μm, and 70 μm, indicating that 10%, 50%, and 90% of the total particle volume consists of particles smaller than these respective sizes. The true density of the powder was determined using a gas pycnometer (Micromeritics AccuPyc II 1345, Norcross, GA, USA) and was found to be 3.21 g/cm3. Figure 1 shows the SEM image of SiC powder and the particle size distribution of SiC powder.
Figure 1.
(a) SEM image of SiC powder [22]; (b) particle size distribution of SiC powder.
2.2. Binder Jetting of Green Parts
Creo Parametric v9.0 (Boston, MA, USA), a computer-aided design (CAD) software, was used to create the 3D model of the parts. This 3D model had dimensions of 22 mm in length, 20 mm in width, and 3.6 mm in thickness. The same software was then employed to export the model as an STL file, which was later converted into G-code to provide the necessary instructions for the printer’s operation.
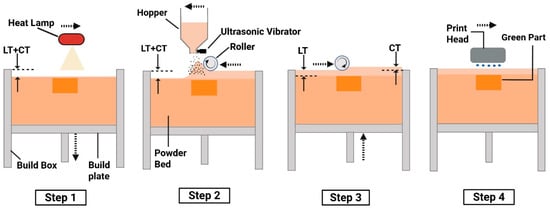
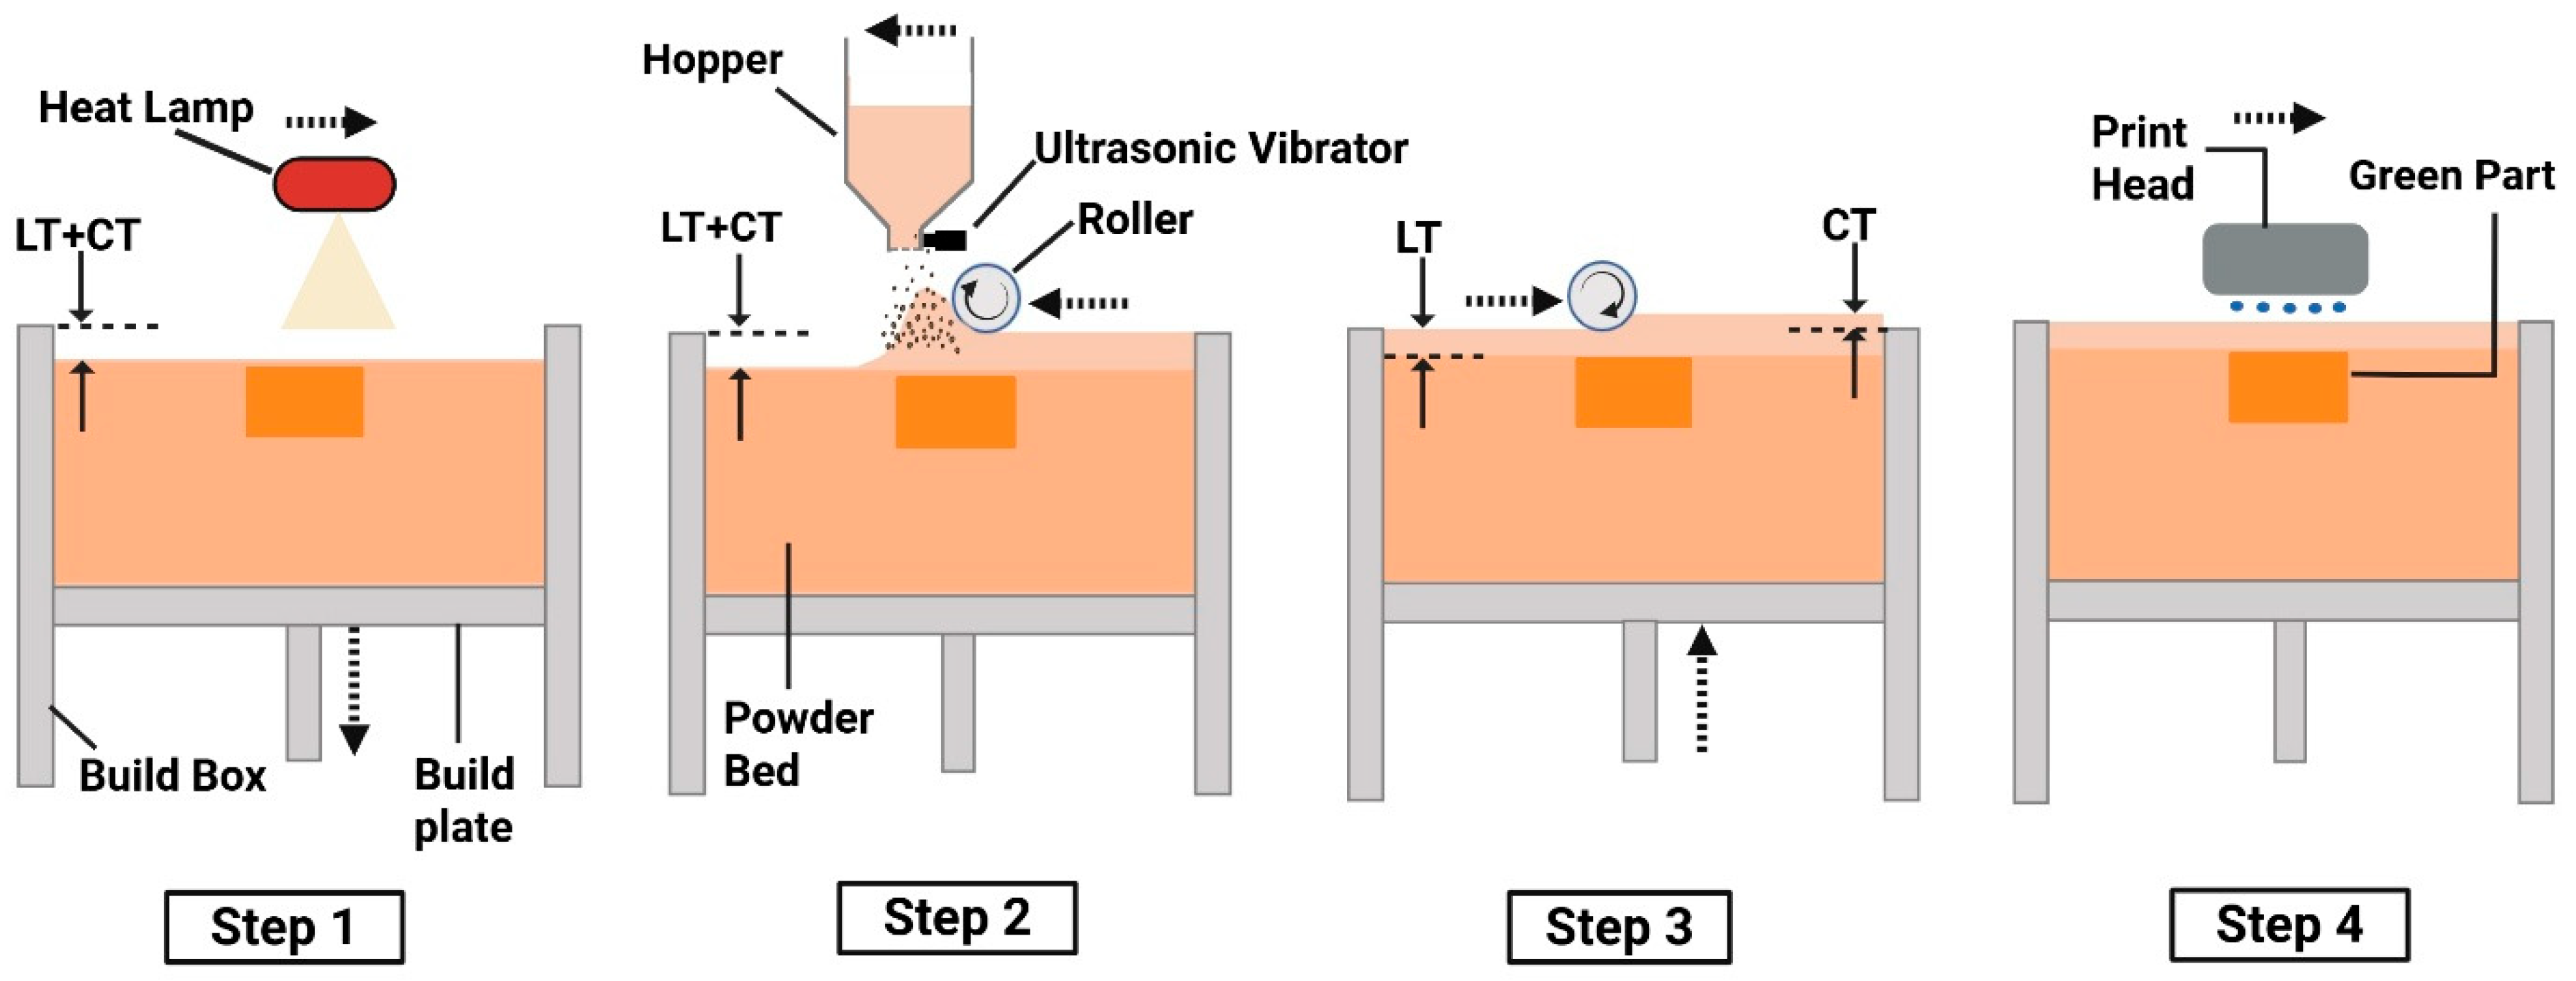
The printing process employed in this study followed the procedures reported in earlier publications [22,23]. Fabrication was performed using a binder jetting system (Innovent+, ExOne Company, North Huntington, PA, USA) together with an aqueous binder (BA005, ExOne Company, North Huntington, PA, USA). Comprehensive descriptions of the printing steps are available in previous studies [22,23]. Figure 2 illustrates the basic steps of the BJAM printing process.
Figure 2.
Basic steps (heating powder bed, dispensing, spreading, and binder jetting) of the binder jetting 3D printing process. Here, LT represents layer thickness, and CT represents compaction thickness [22].
The variables that were kept fixed in the study are presented in Table 2. The definitions of these variables can be found in the literature [11,12,13]. Preliminary trials were conducted to determine the values for each of these variables, focusing on achieving good powder bed quality (e.g., minimal surface defects on powder bed) and ensuring that the green parts had sufficient strength for subsequent processing steps (such as curing and debinding).
Table 2.
Fixed printing variables and their values.
The variables that were changed in the study are binder saturation (%) and drying time. Their values are presented in Table 3. A partial replication design was employed. To evaluate variations under the same conditions, two replications were conducted only for binder saturation 100% and drying time 15 s, while no replication was performed for other experimental conditions [24].
Table 3.
Levels of variables at each experimental condition.
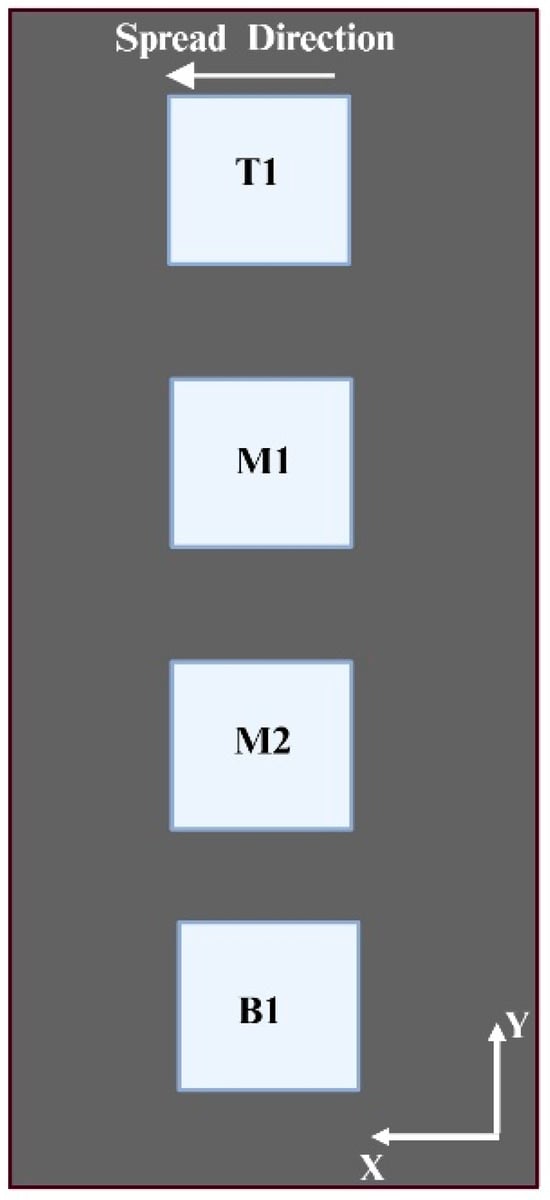
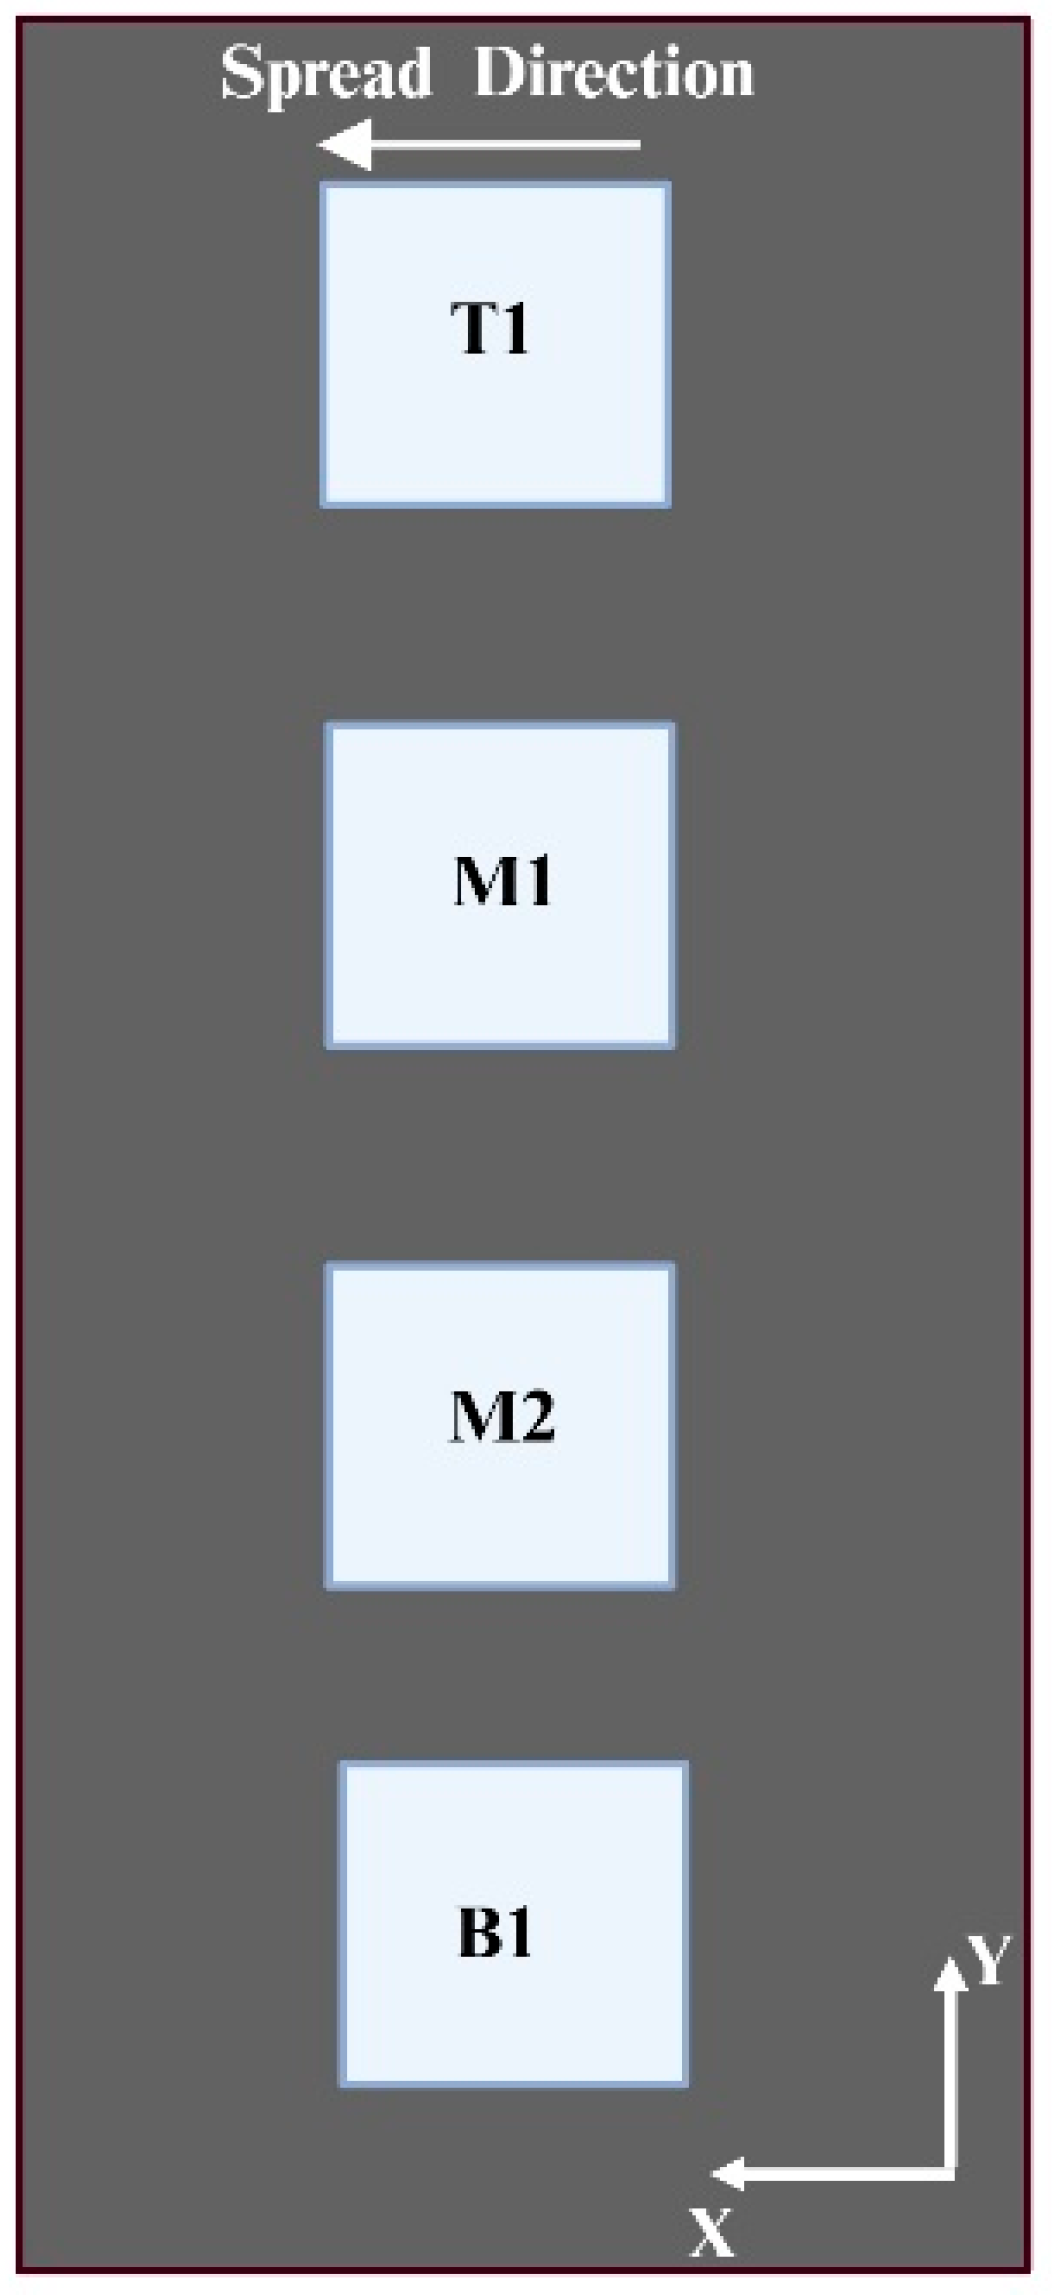
In each experimental condition, four parts were printed. Their positions on the build plate are illustrated in Figure 3, with the part thickness aligned in the build (Z) direction. Each part was labeled according to its placement on the build plate: “T1” for the top region, “M1” and “M2” for the middle region, and “B1” for the bottom region. In the figure, the X-direction, also referred to as the spread direction, represents the path along which the roller spreads powder from right to left during the dispensing and spreading step (as shown in Figure 3).
Figure 3.
Labels and locations of the printed parts on the build plate.
The position of a printed green part on the build plate can affect its density, and notable density differences may occur among parts produced in the same experimental run on the printer used in this study [22,23,25]. Printing multiple parts in a single run could therefore introduce excessive variation in the density measurements. To avoid this potential source of error, only one part from each condition—specifically, the part located at position M1 shown in Figure 3—was included in the data analysis.
Following printing, the build box containing the printed parts along with the surrounding loose powder was placed in an oven (DX402C, Yamato Scientific, Tokyo, Japan) and heated at 125 °C for 5 h to cure the binder within the green parts. This curing step was carried out to enhance the mechanical strength of the green parts before the step of de-powdering [22].
2.3. Measurement of Dimensional Deviation of Green Parts
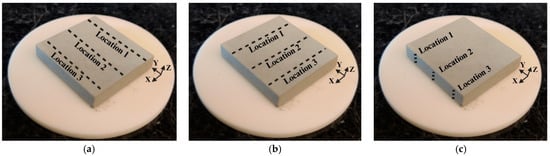
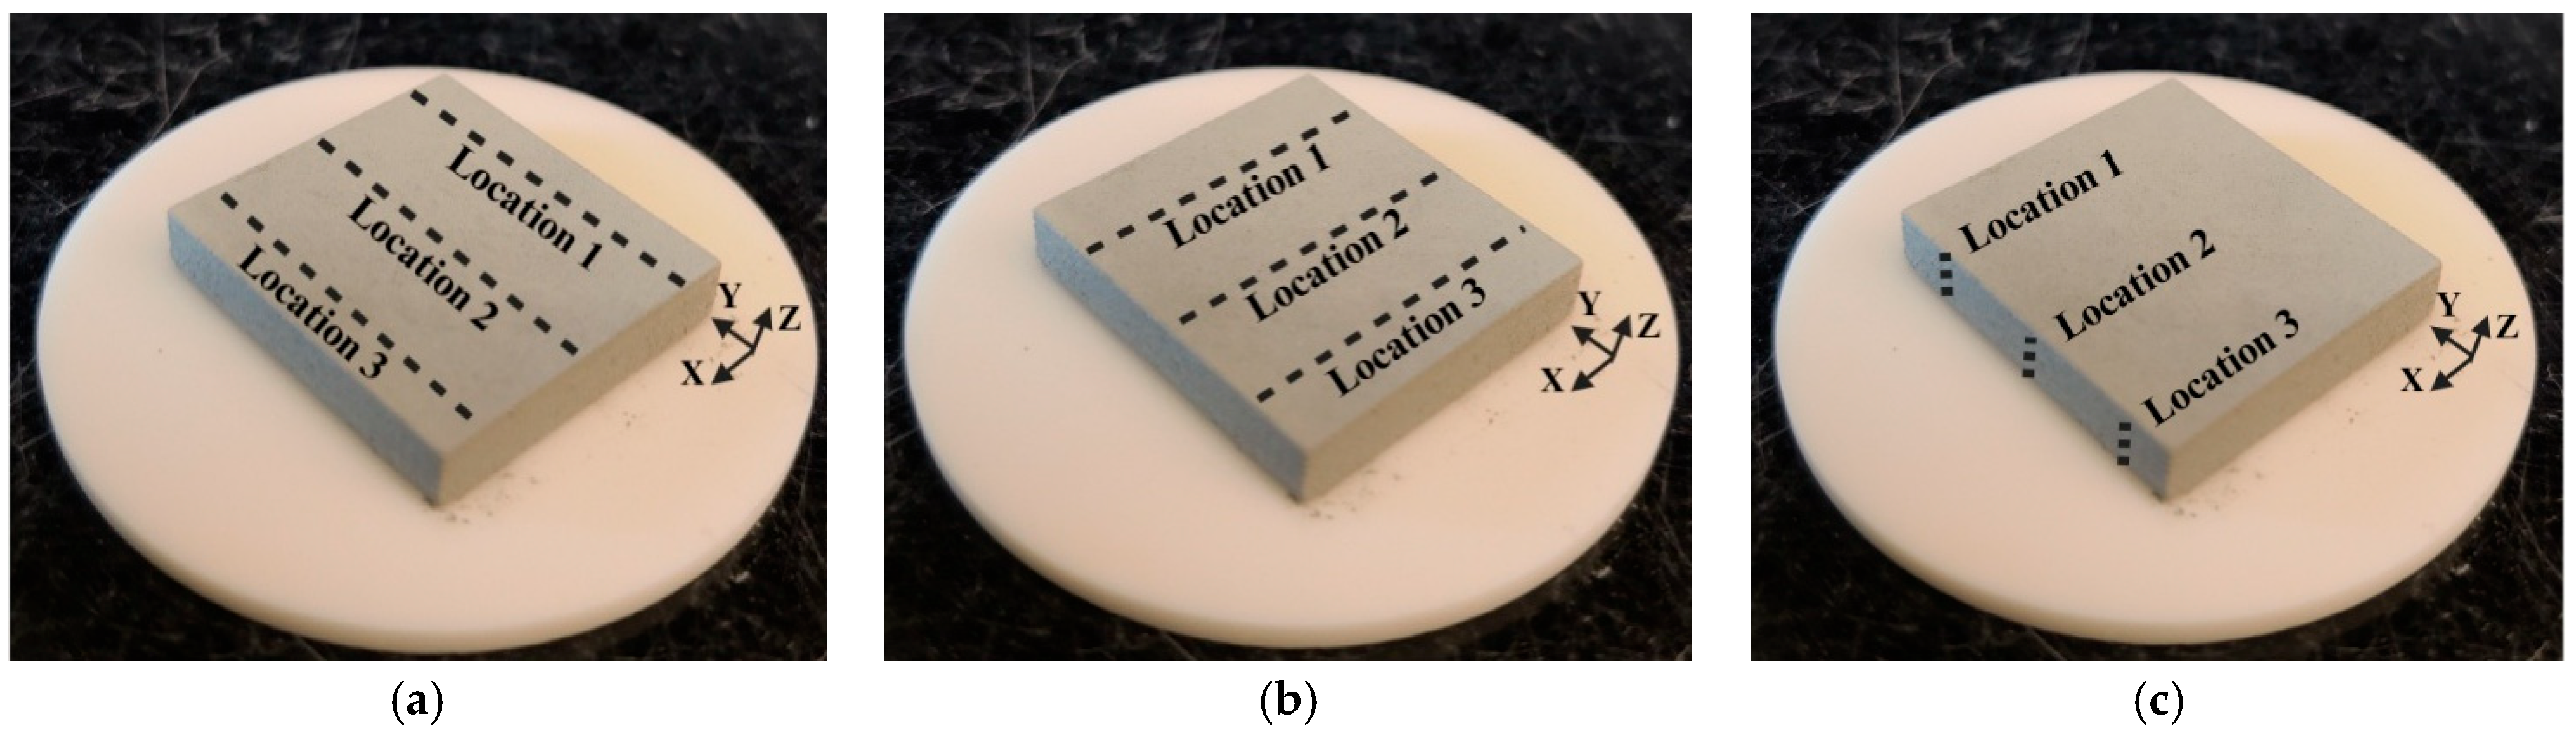
Dimensional deviation of the green parts was calculated using Equation (1). Three dimensions—length, width, and thickness—were measured on each part using a slide caliper (Mitutoyo 500-196-30 Digimatic 0–6′′/150 MM stainless steel digital caliper, Kawasaki, Japan). For each dimension, three measurements (D1, D2, and D3) were taken at three different locations shown in Figure 4. The average of these three measurements () was then used in the calculation.
where = (D1 + D2 + D3)/3 and = dimension from the CAD model. Equation (1) was applied separately to length, width, and thickness to obtain their respective dimensional deviations.
Figure 4.
Measurement locations on green parts: (a) length, (b) width, and (c) thickness.
2.4. Measurement of Density of Green Parts
Green density () of the printed parts, defined as the mass per unit volume of the parts, was calculated using Equation (2). The density measurement method used in this study has been used in previous studies on binder jetting of silicon carbide powder [22,23]. Within Equation (2), m represents the mass of the part and was measured with a scale that had a resolution of 0.001 g. l, , and denote the length, width, and thickness of the green part, respectively. These three dimensions were measured as described in Section 2.3.
3. Result and Discussion
3.1. Effect of Binder Saturation
3.1.1. Effect of Binder Saturation on Dimensional Deviation of Green Parts
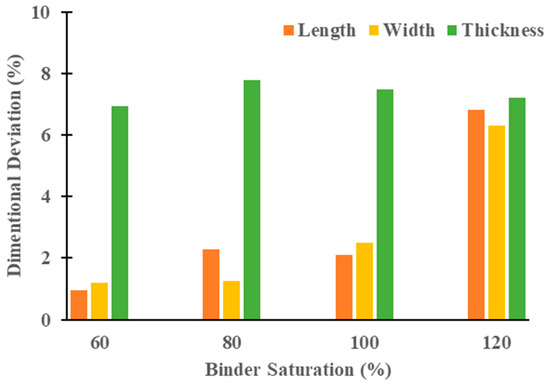
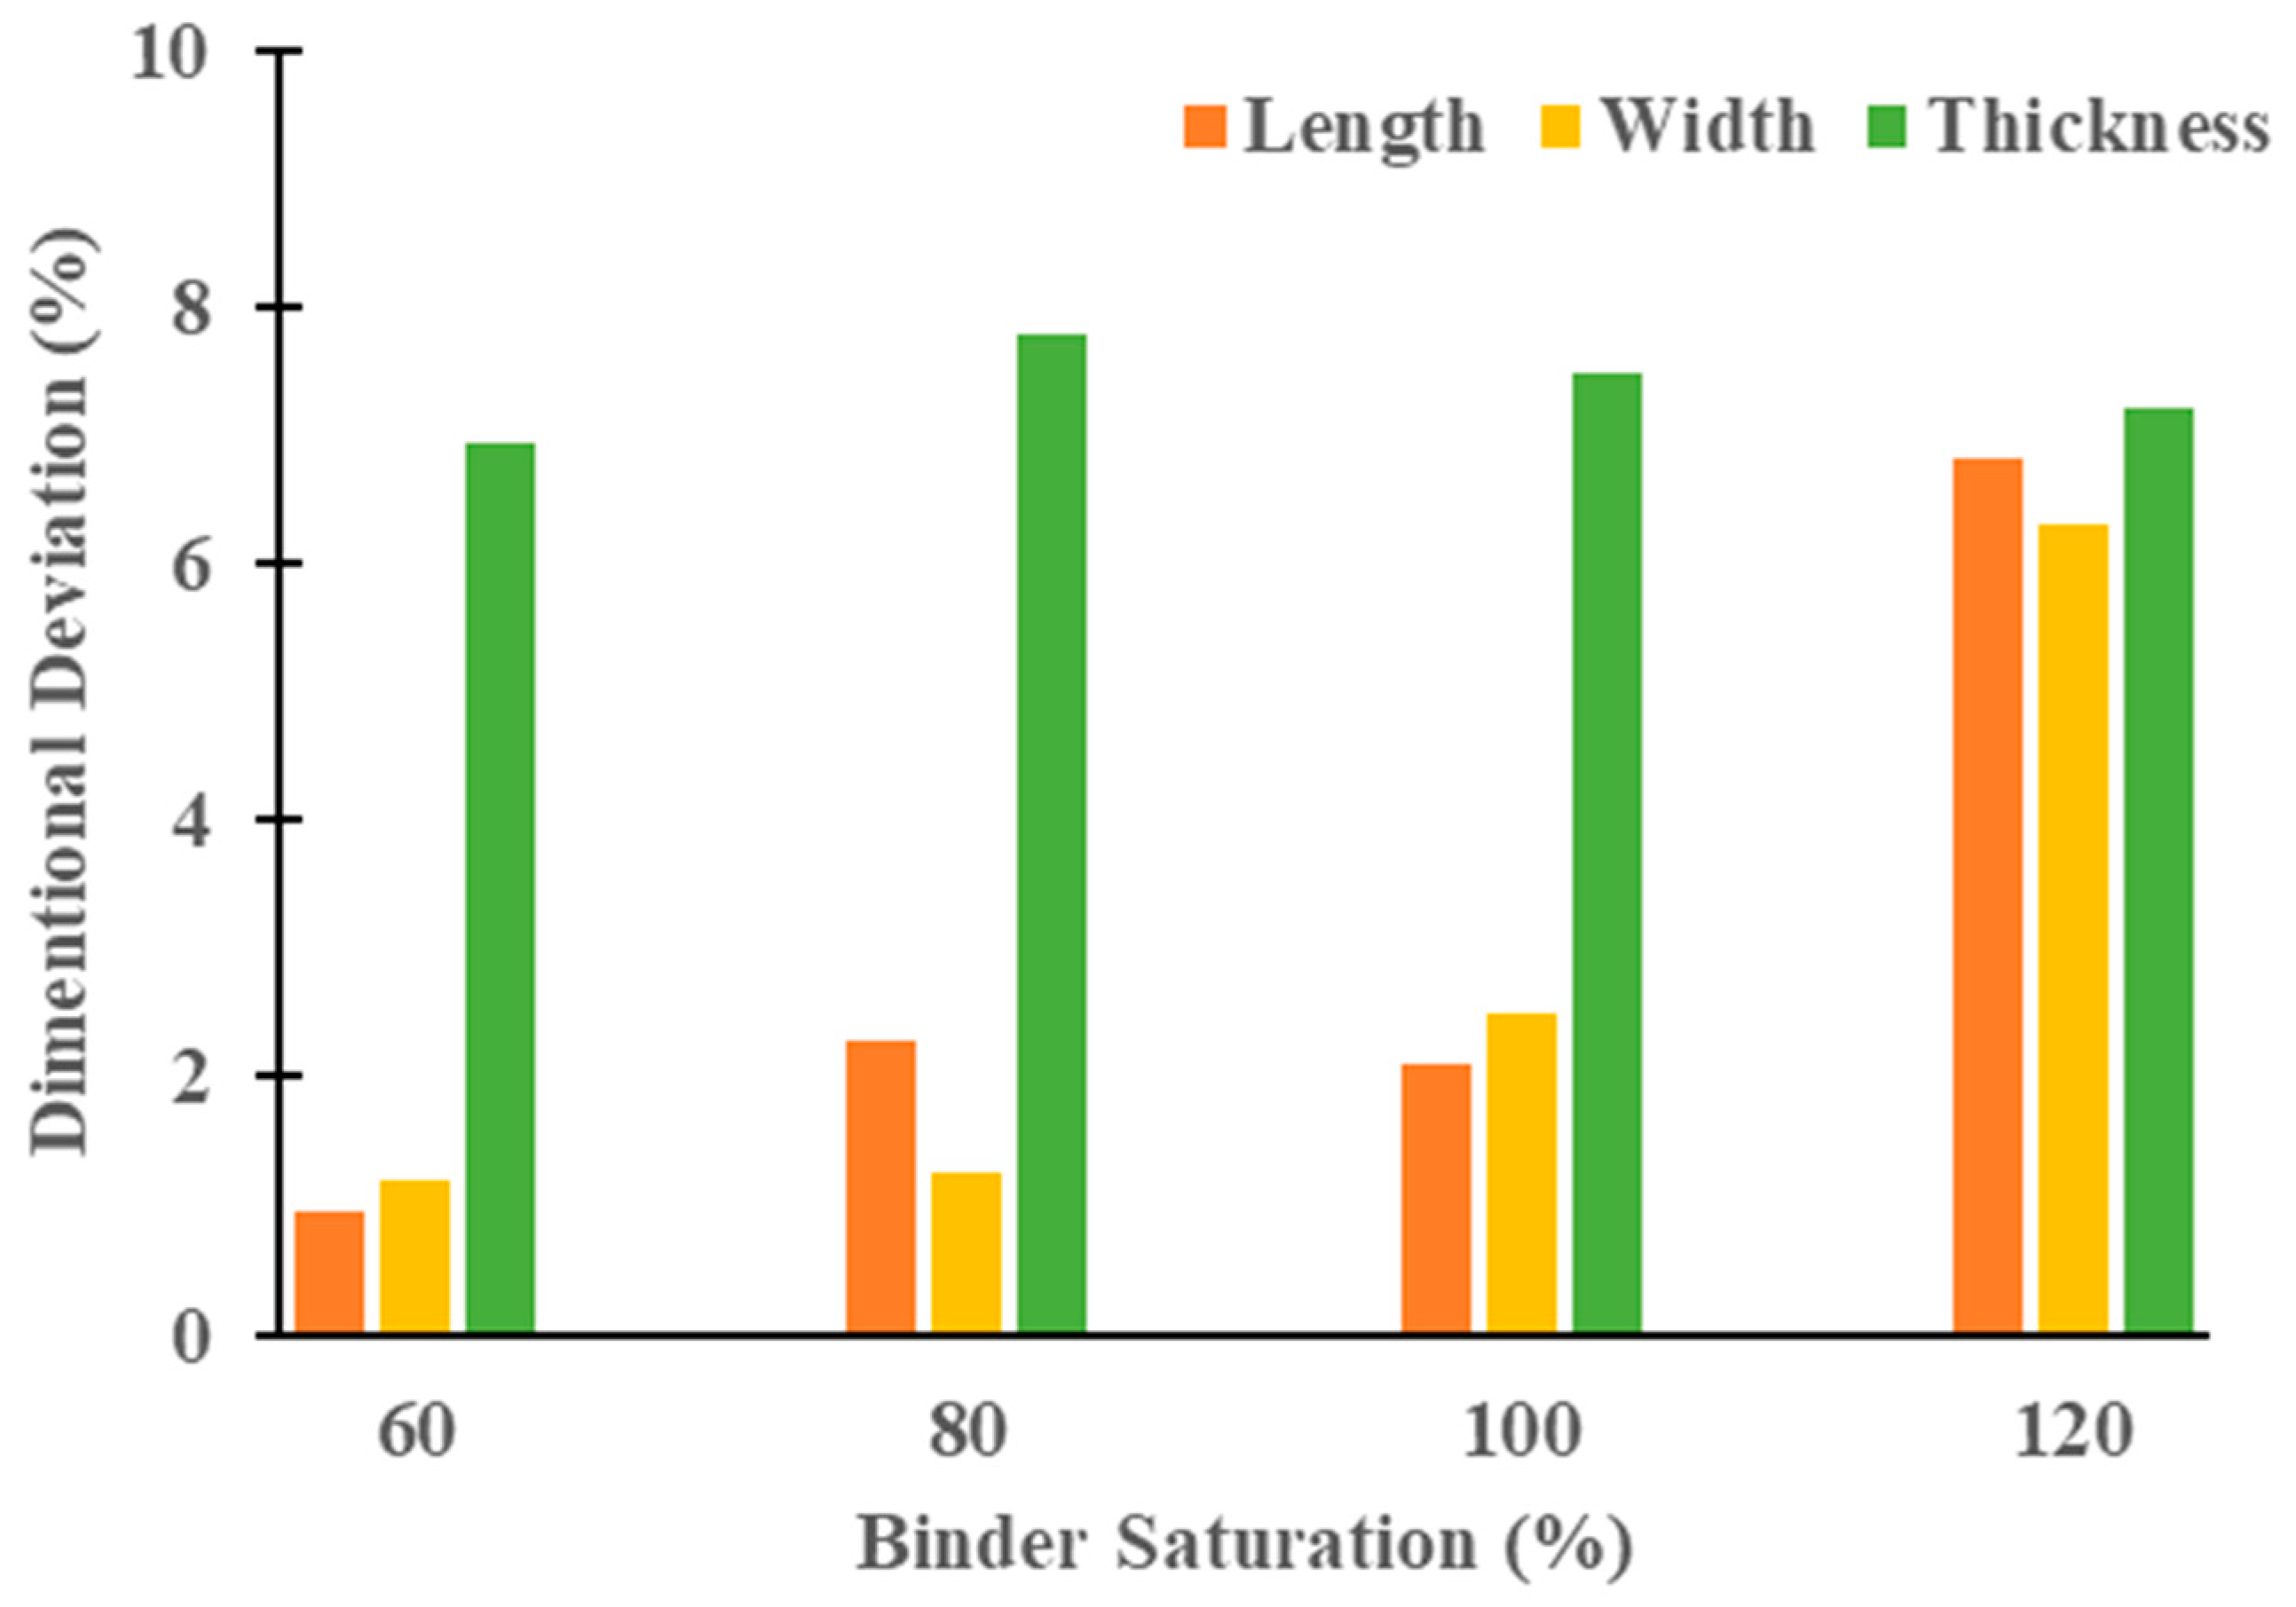
Figure 5 shows the dimensional deviation in length, width, and thickness of green parts printed at binder saturation levels of 60%, 80%, 100%, and 120% at a fixed drying time of 15 s. Across all binder saturation levels, thickness showed the highest deviation, ranging from approximately 7% to 7.8%. Length and width deviations remained below 2% for saturation levels up to 100%, but increased to about 6.6% and 6%, respectively, at 120% saturation. The consistently high deviation in thickness compared to length and width indicates that dimensional deviation was more pronounced in the build direction.
Figure 5.
Effect of binder saturation on dimensional deviation of green parts at a drying time of 15 s.
As shown in Figure 5, increasing binder saturation level leads to increased dimensional deviation of the green parts. This trend aligns with trends observed in reported binder jetting studies [17,19,26]. For example, Miyanaji et al. demonstrated that dimensional deviation increased with a higher level of binder saturation when printing metal powder (Ti-6Al-4V) [17]. Vaezi and Chua reported that increasing the binder saturation level increased dimensional deviation (measured using stereomicroscope imaging) of green parts when using a plaster-based powder (ZP102) [19]. Hodder et al. also observed an increase in dimensional deviation (assessed by qualitative visual inspection) at elevated binder saturation using sand-based powder (silica sand) [26]. While these reported studies were conducted using metallic powder, plaster-based powder, or sand-based powder, the present study was conducted using SiC ceramic powder. Additionally, unlike reported studies that evaluated dimensional deviation using microscopic image analysis or qualitative visual inspection, dimensional deviation in this study is measured using a slide caliper.
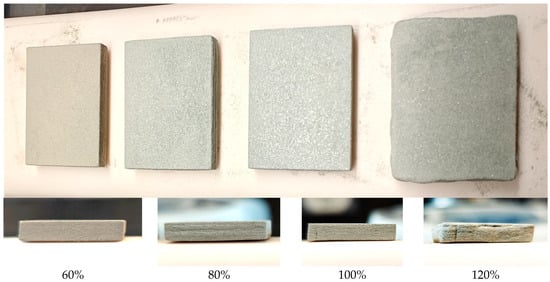
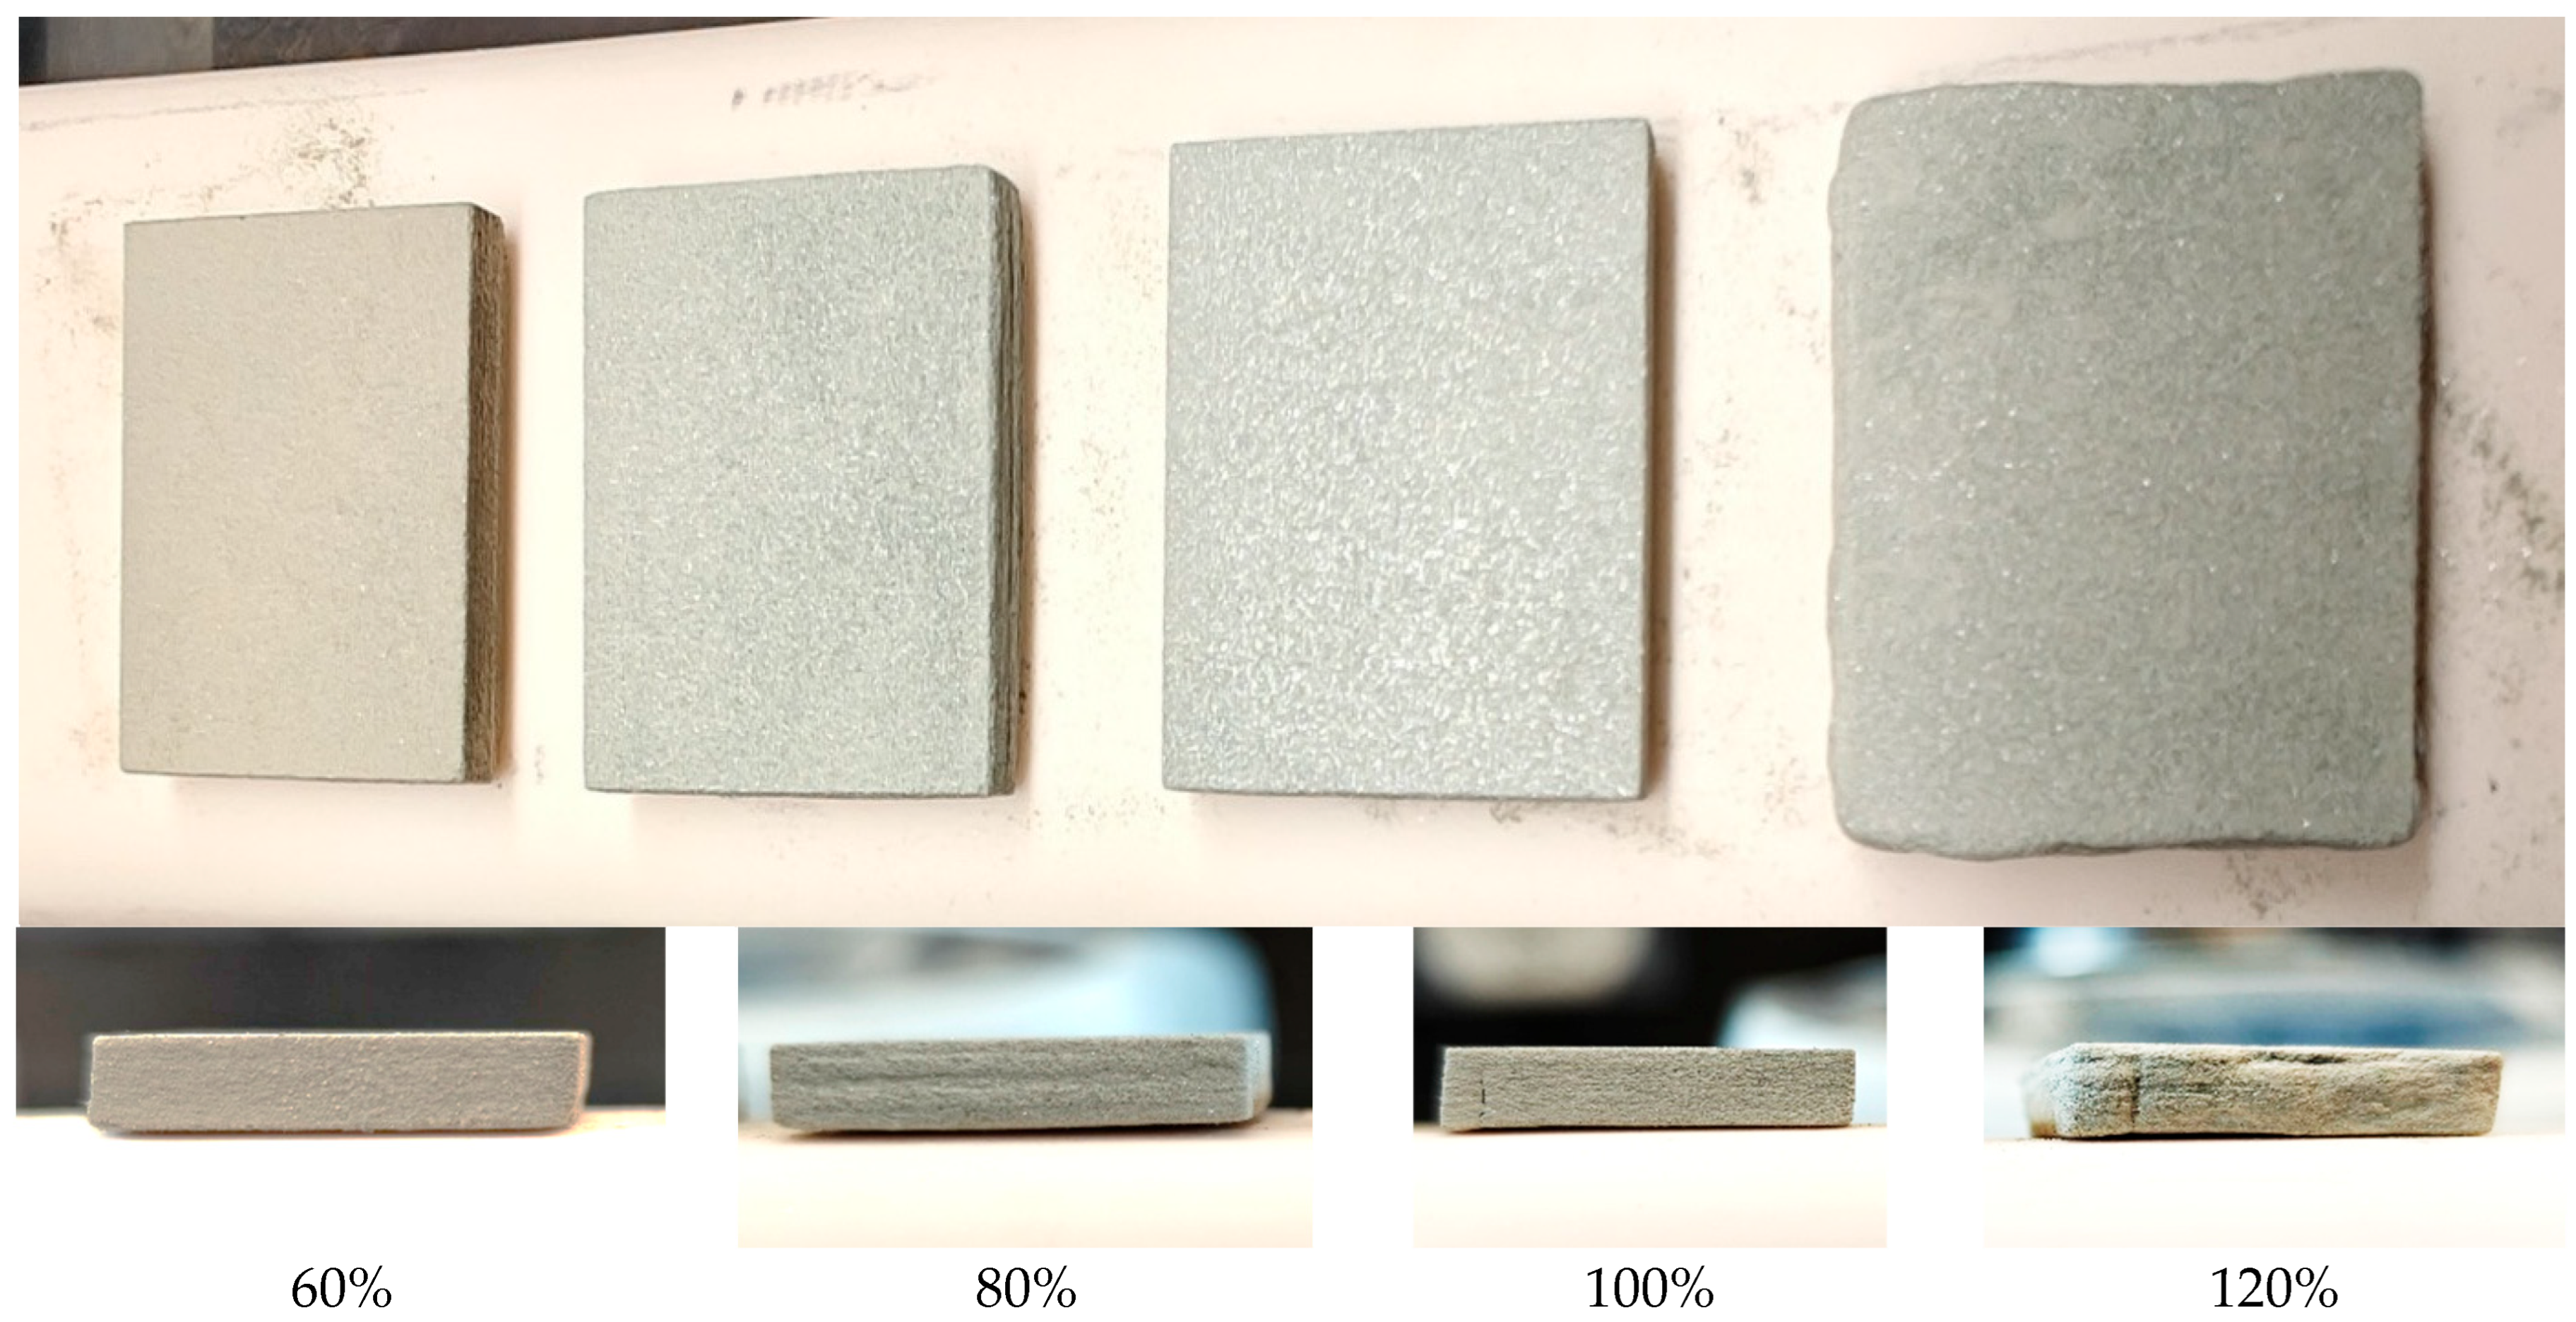
These results highlight the critical role of binder saturation in maintaining minimal dimensional deviation in binder jetting. The visual evidence in Figure 6 supports this observation. The first three parts (from left to right), corresponding to 60%, 80%, and 100% saturation, maintain sharp edges and consistent surface quality. In contrast, the part at 120% saturation (far right) exhibits noticeable swelling, edge deformation, and surface irregularities, confirming the negative effects of excessive binder content on dimensional deviation.
Figure 6.
Images of green parts at different levels of binder saturation.
3.1.2. Effect of Binder Saturation on Density of Green Parts
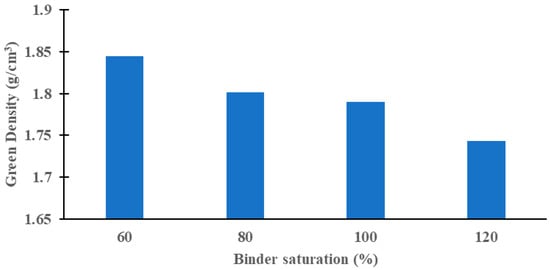
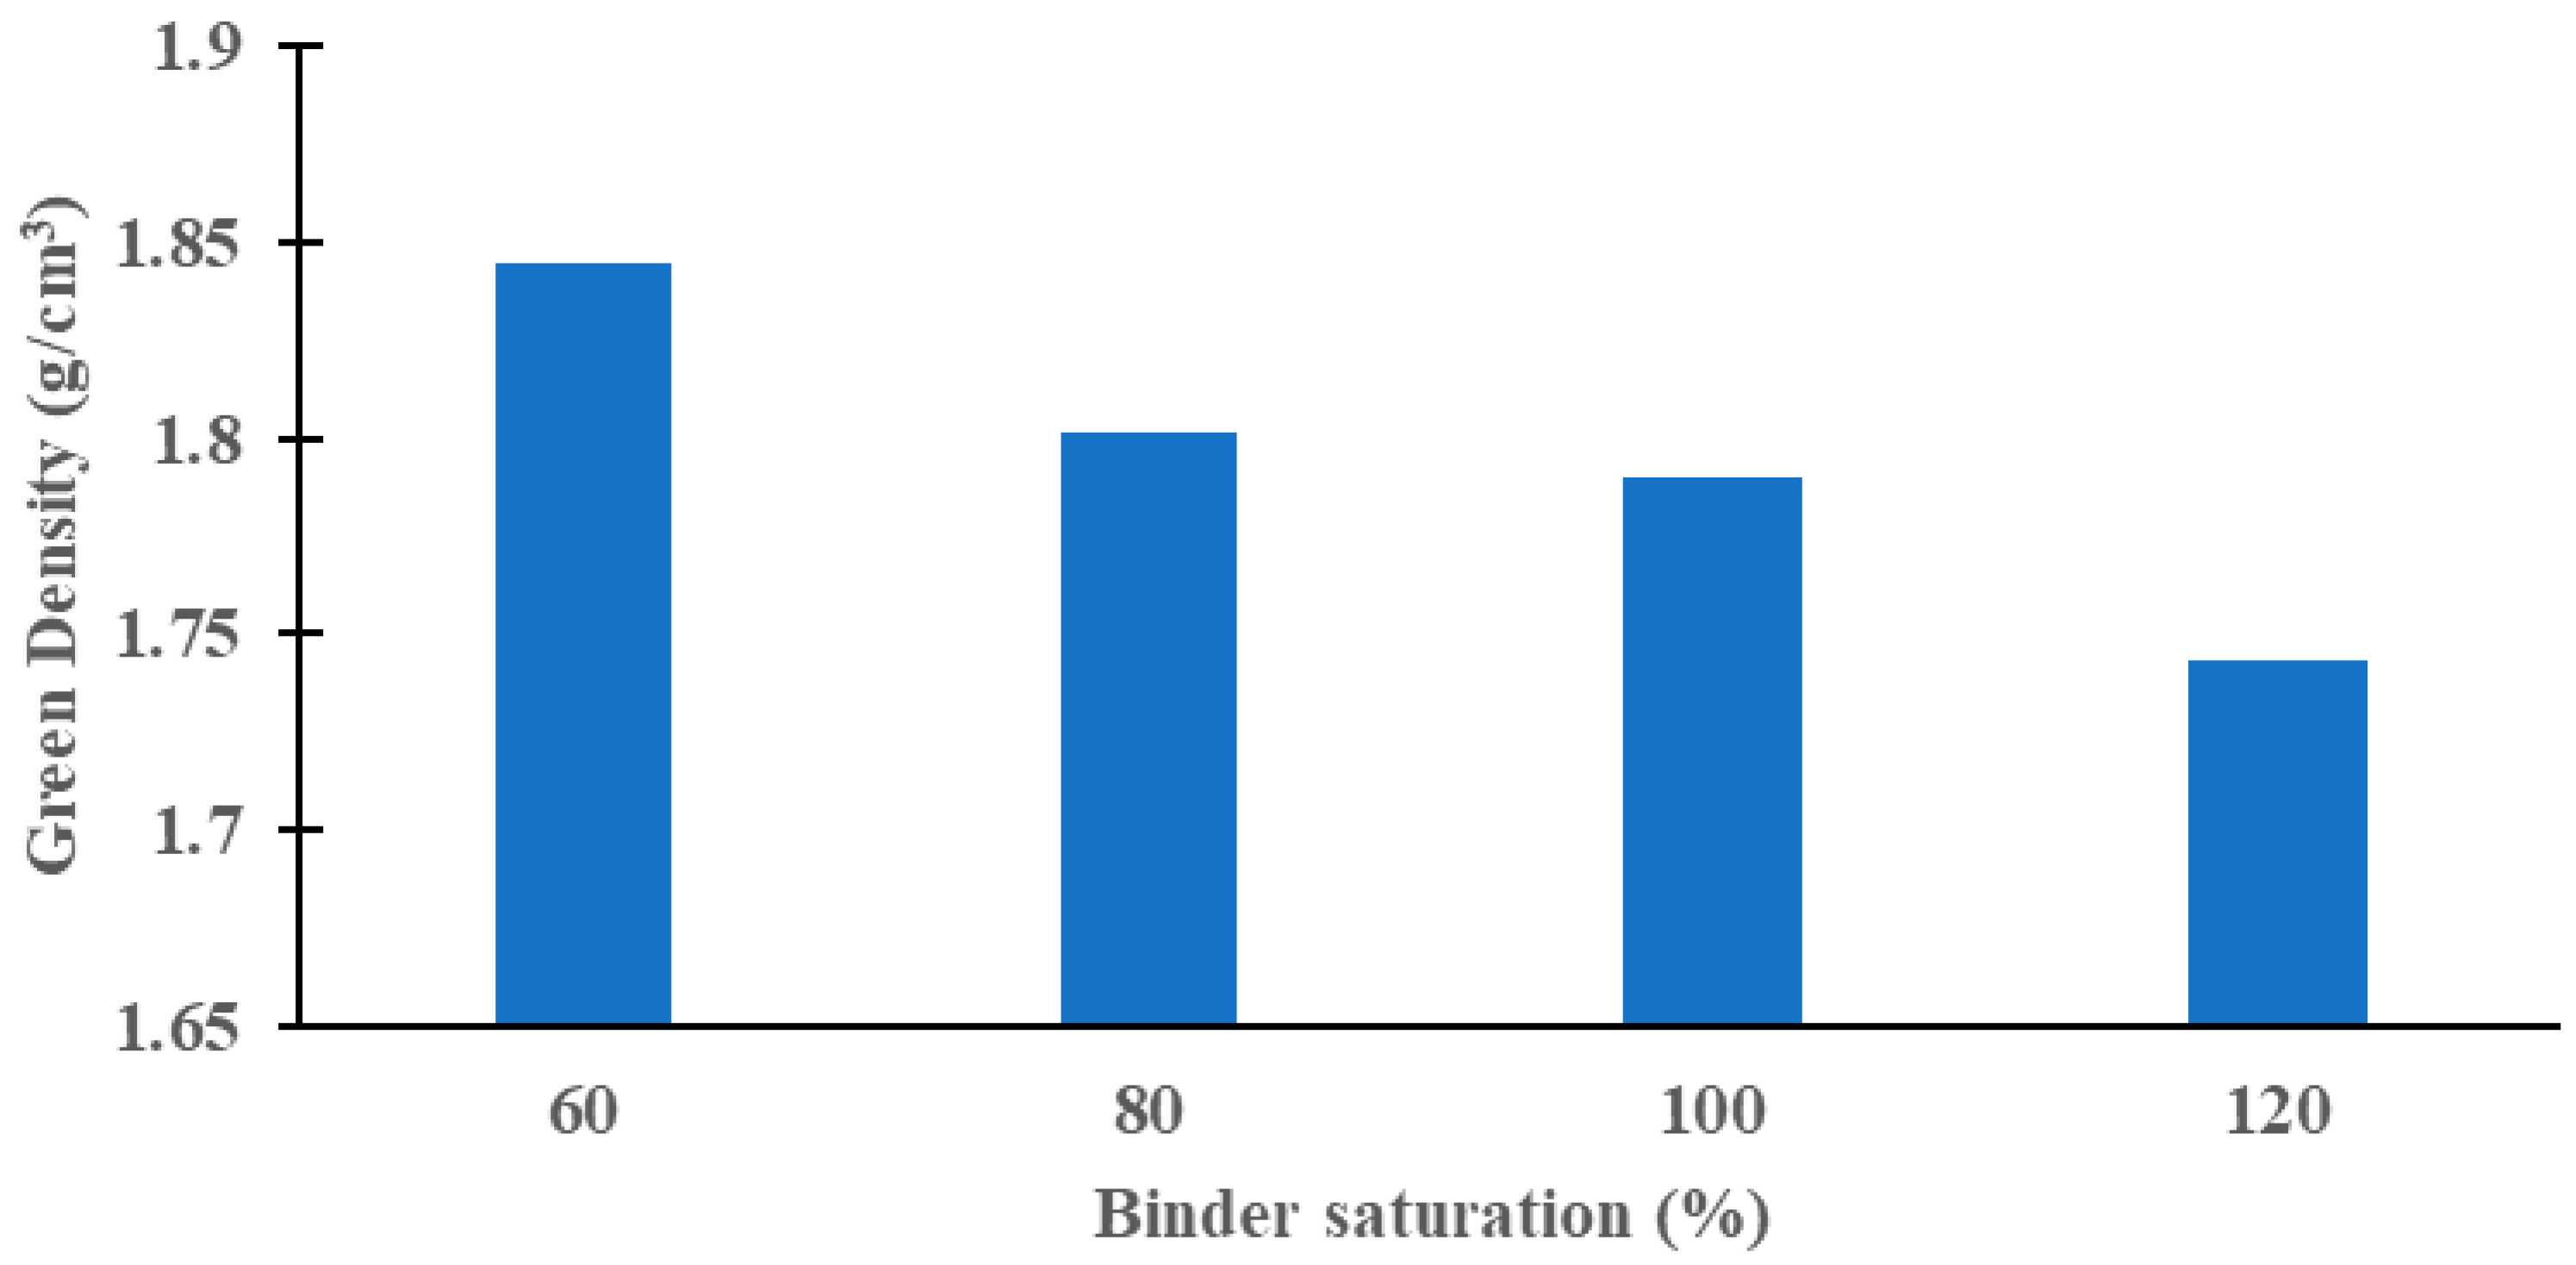
Figure 7 shows the effect of binder saturation on the green part density. As binder saturation increased from 60% to 120%, a decreasing trend in density was observed. The highest density, approximately 1.85 g/cm3, was achieved at 60% saturation, while the lowest density, around 1.73 g/cm3, was recorded at 120% saturation. This inverse relationship suggests that excessive binder content may lead to over-wetting and binder bleeding, which can disrupt powder packing and increase porosity. In contrast, lower binder saturation appears to support more uniform binder distribution, resulting in higher green part density. This trend is consistent with trends observed in some reported studies [15,16], but is in contrast to the trend observed in one reported study [15]. Mostafaei et al. reported that, when binder jetting using WC–Co composite powder, green density decreased with increasing binder saturation at a drying time of 30 s, whereas an opposite trend was observed at a drying time of 45 s, indicating a strong interaction between binder saturation and drying time [15]. Additionally, Huang et al. reported an increasing trend in green density with higher binder saturation for ZrO2 ceramic powder [16]; however, their study employed much lower binder saturation levels (7–17%). These results indicate that the effects of binder saturation on the density of green parts are dependent on the powder material and other process variables (such as drying time).
Figure 7.
Effect of binder saturation on the density of green parts.
3.2. Effect of Drying Time
3.2.1. Effect of Drying Time on Dimensional Deviation of Green Parts
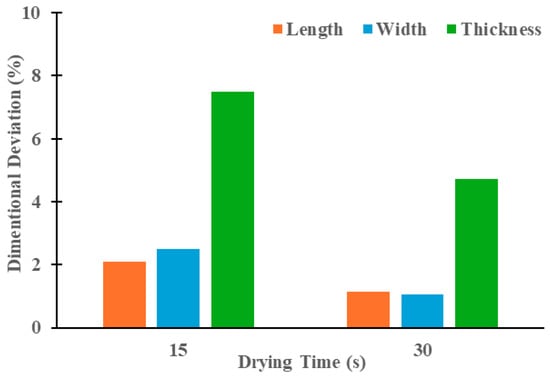
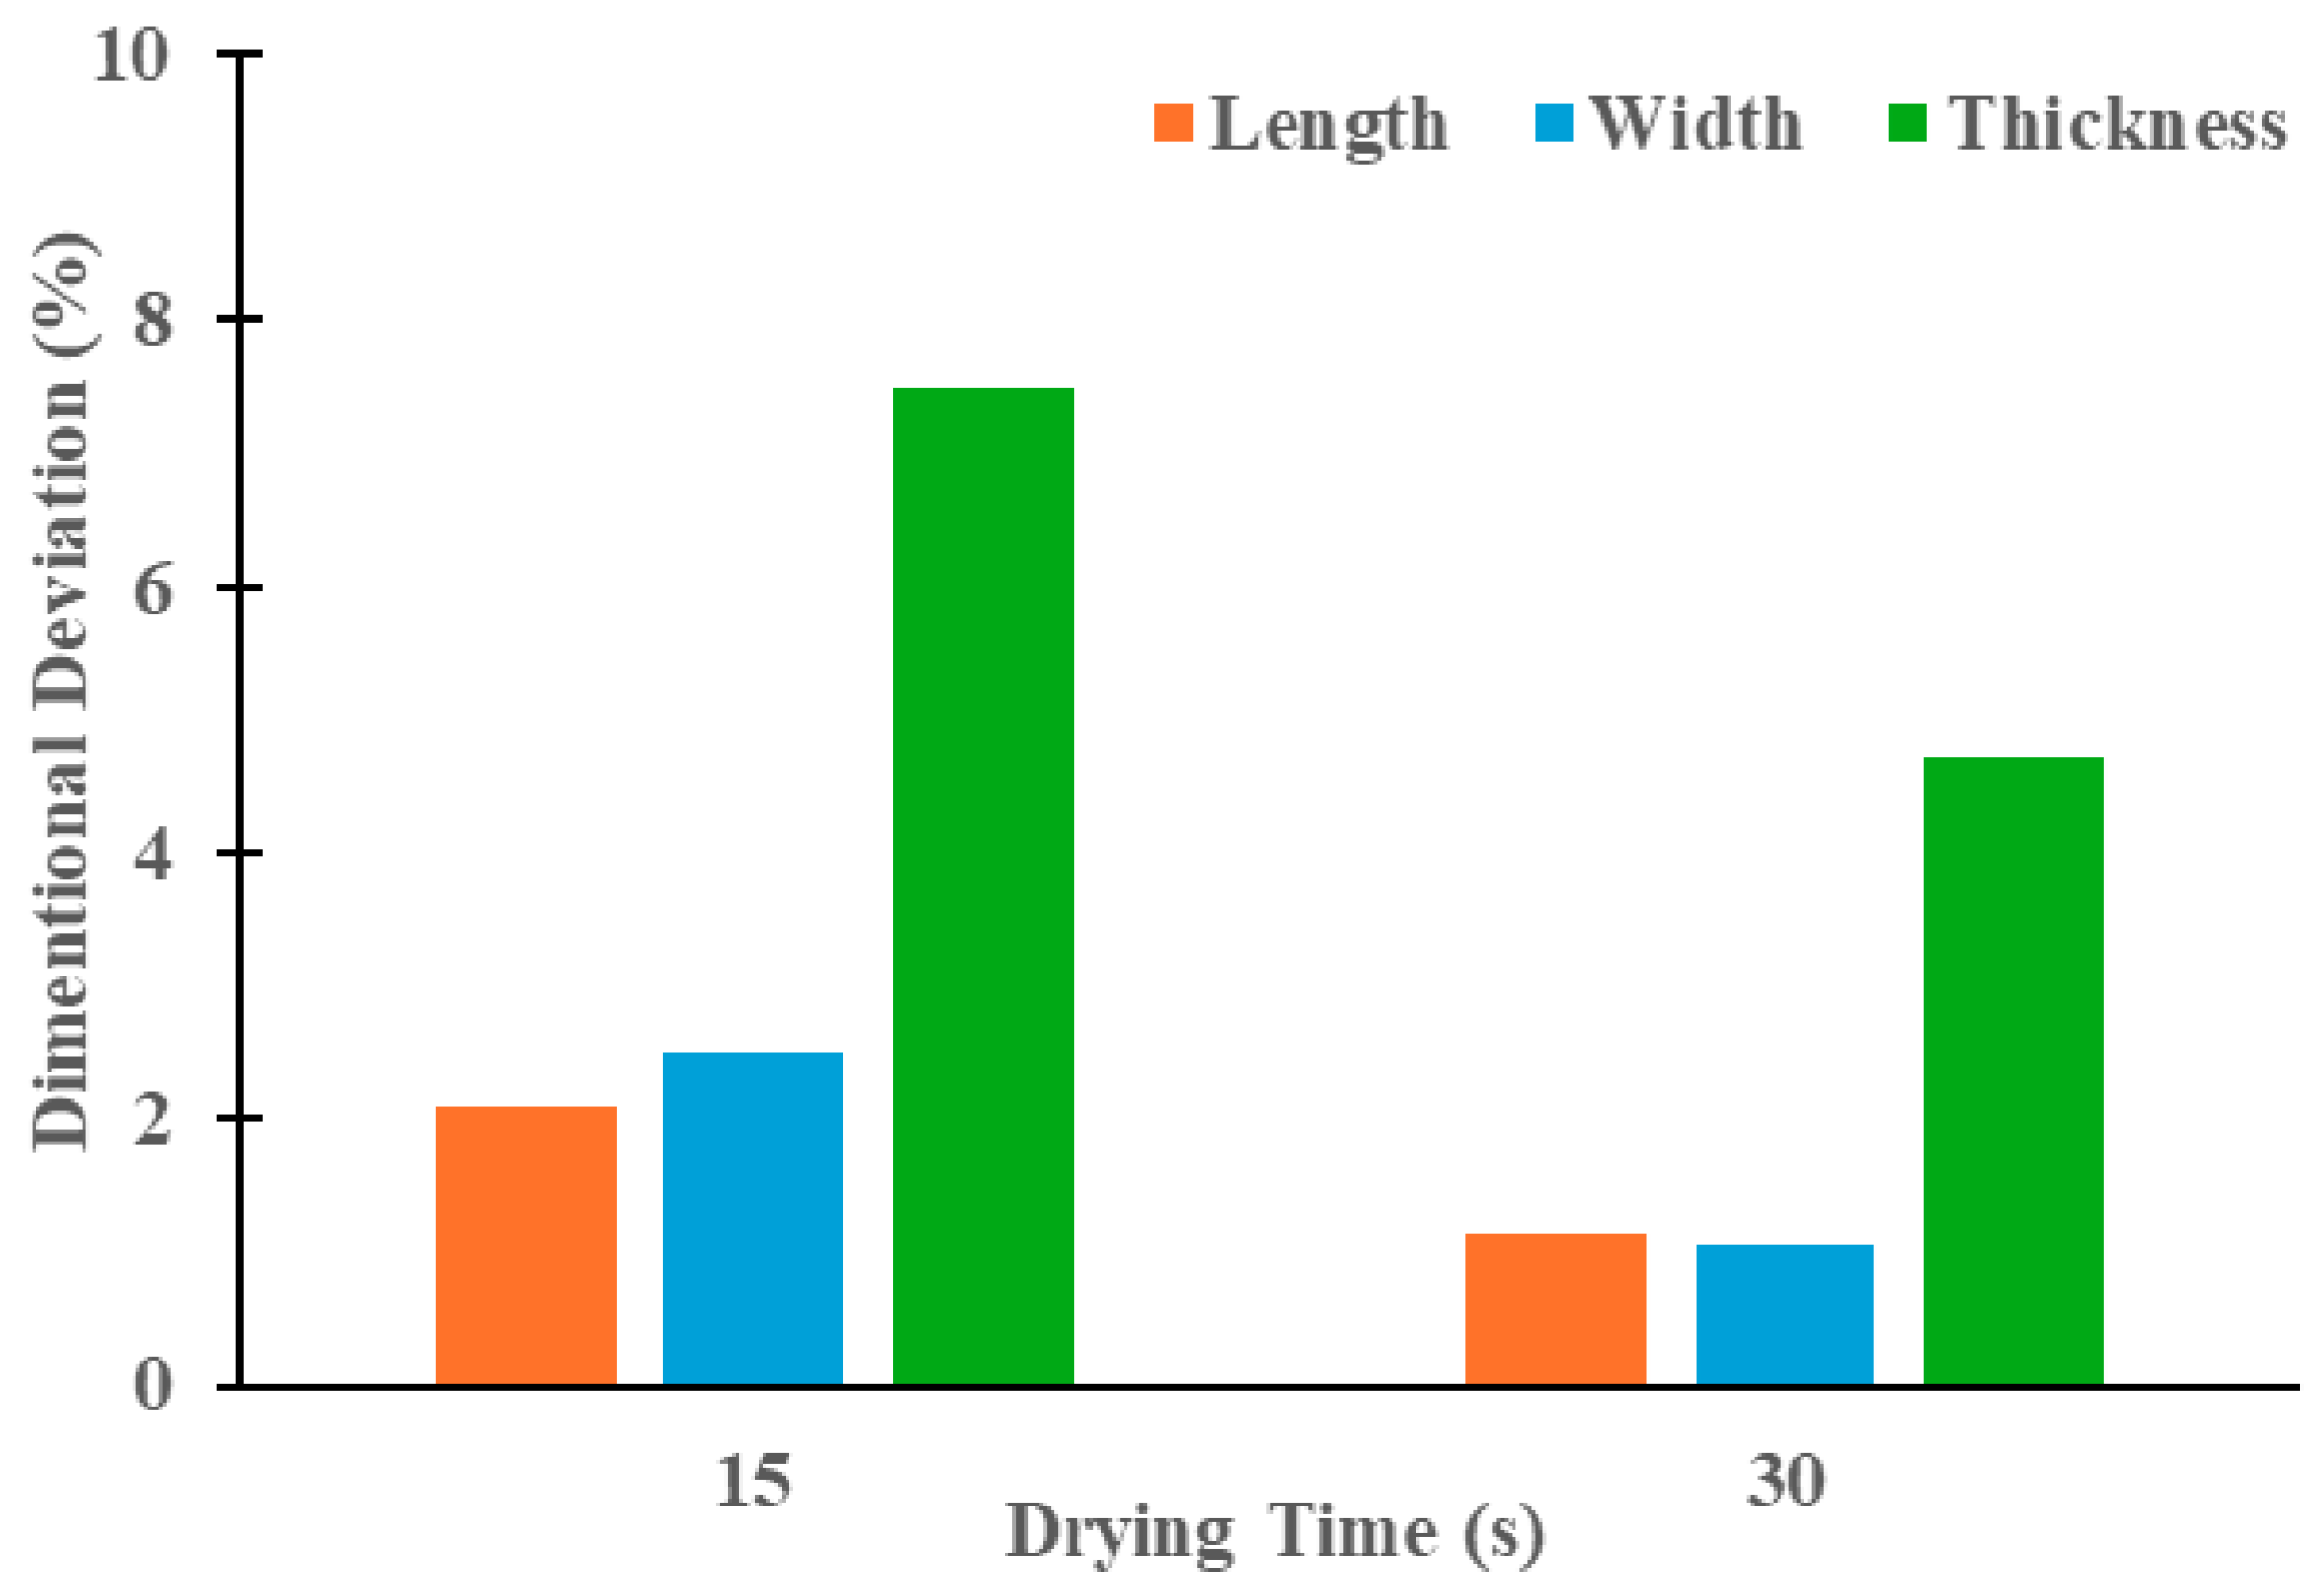
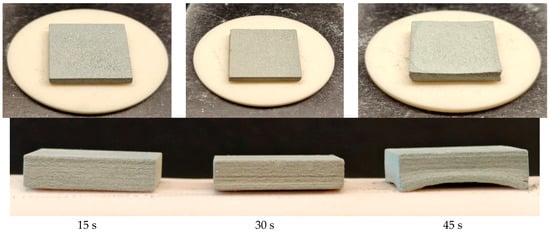
Figure 8 shows the effect of drying time on dimensional deviation of green parts in length, width, and thickness at a binder saturation level of 100%. At a drying time of 15 s, thickness exhibited the highest deviation at approximately 7.4%, while length and width deviations were much lower, around 2.0% and 2.4%, respectively. When the drying time increased to 30 s, deviations in all dimensions decreased, with thickness dropping to about 4.5% and length and width both remaining close to 1%. Increasing the drying time from 15 s to 30 s resulted in a substantial reduction in dimensional deviation. However, further increasing the drying time to 45 s led to severe warpage, as shown in Figure 9; therefore, dimensional values for this condition are excluded. This non-linear behavior is consistent with findings reported by Miyanaji et al. [12], who investigated the effects of drying time on dimensional deviation at three levels of drying time (30 s, 45 s, and 60 s). Miyanaji et al. reported that through statistical analysis, drying time had a statistically significant effect on green part dimensional deviation in the X, Y, and Z directions, with dimensional deviation improving at a drying time level of 45 s but deteriorating at longer drying times. Unlike the study by Miyanaji et al. using porcelain, where excessive drying led to gradual increases in dimensional deviation, the present SiC study shows that excessive drying causes severe warpage and loss of geometric integrity.
Figure 8.
Effect of drying time on dimensional deviation of green parts at binder saturation of 100%.
Figure 9.
Images of green parts at different levels of drying time.
3.2.2. Effect of Drying Time on Density of Green Parts
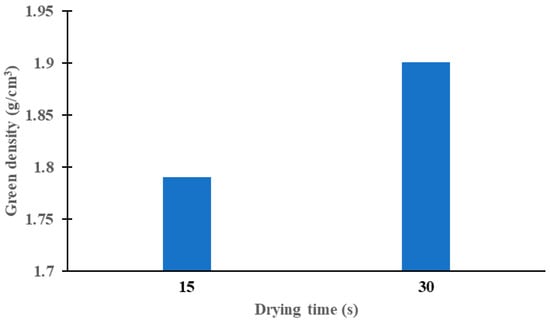
Figure 10 shows the effect of drying time on the density of green parts. As the drying time increased from 15 s to 30 s, the green density increased from approximately 1.78 g/cm3 to 1.90 g/cm3. This trend aligns with the trend observed in the reported study on binder jetting conducted by Mostafaei et al. [15]. They reported that when binder jetting WC–Co composite powder, extended drying time led to increased green part density.
Figure 10.
Effect of drying time on the density of green parts. The density value corresponding to the drying time of 45 s is not included, as no dimensionally accurate green part was printed.
It can be assumed that increasing drying time allows the binder to fully solidify and evenly bond powder particles, reducing voids and improving cohesion, which leads to higher green part density.
4. Conclusions
In this study, the effects of binder saturation and drying time on the dimensional deviation and density of silicon carbide (SiC) green parts printed by binder jetting additive manufacturing (BJAM) were evaluated. As binder saturation increased from 60% to 120%, green density decreased from 1.85 g/cm3 to 1.73 g/cm3, while dimensional deviation increased significantly. Increasing drying time from 15 s to 30 s reduced dimensional deviation and improved green density to 1.90 g/cm3; however, prolonged drying time at 45 s caused severe warpage and prevented the formation of dimensionally accurate parts. These results emphasize the need to optimize binder saturation and drying time to ensure desired density with minimal dimensional deviation in BJAM-printed SiC green parts. Future studies will include SEM-based microstructural analysis of green parts to investigate binder distribution, particle bonding, and pore morphology, providing insight into the effects of binder saturation and drying time on density and dimensional deviation of green parts. Future work will also extend the present study through a full factorial design to quantify the individual and interaction effects of binder saturation and drying time, followed by response surface methodology (RSM)-based optimization to determine the best combination of binder saturation and drying time to get the desired density while maintaining minimal dimensional deviation of SiC green parts. Future work will also incorporate FEM and theoretical modeling.
Author Contributions
Conceptualization, M.M.P. and Z.P.; methodology, M.M.P. and Z.P.; formal analysis, M.M.P.; experiment, M.M.P. and M.S.A.; resources, Z.P. and S.K.; data curation, M.M.P. and Z.P.; writing—original draft preparation, M.M.P.; writing—review and editing, Z.P., M.M.P., M.S.A. and S.K. All authors have read and agreed to the published version of the manuscript.
Funding
This research received no external funding.
Data Availability Statement
The authors confirm that the data that support the findings of this study are available within the article or upon request to the corresponding author.
Acknowledgments
The authors would like to acknowledge Steven Kuntzendorf (Undergraduate student, Department of Industrial & Systems Engineering, Texas A&M University, College Station, TX 77843, USA) for his assistance in conducting the experiment in this paper.
Conflicts of Interest
Authors Mostafa Meraj Pasha, Zhijian Pei, and Md Shakil Arman are employed by Texas A&M University, College Station, and Stephen Kachur is employed by the company CPS Technologies Corp. The authors declare that the research was conducted in the absence of any commercial or financial relationships that could be construed as a potential conflict of interest.
References
- Boretti, A.; Castelletto, S. A perspective on 3D printing of silicon carbide. J. Eur. Ceram. Soc. 2024, 44, 1351–1360. [Google Scholar] [CrossRef] [Scilit]
- Eom, J.-H.; Kim, Y.-W.; Raju, S. Processing and properties of macroporous silicon carbide ceramics: A review. J. Asian Ceram. Soc. 2013, 1, 220–242. [Google Scholar] [CrossRef] [Scilit]
- Polozov, I.; Razumov, N.; Masaylo, D.; Silin, A.; Lebedeva, Y.; Popovich, A. Fabrication of silicon carbide fiber-reinforced silicon carbide matrix composites using binder jetting additive manufacturing from irregularly-shaped and spherical powders. Materials 2020, 13, 1766. [Google Scholar] [CrossRef] [Scilit]
- Steibel, J. Ceramic matrix composites taking flight at GE Aviation. Am. Ceram. Soc. Bull 2019, 98, 30–33. [Google Scholar]
- Zhu, D. Aerospace Ceramic Materials: Thermal, Environmental Barrier Coatings and SiC/SiC Ceramic Matrix Composites for Turbine Engine Applications; Glenn Research Center: Sandusky, OH, USA, 2018. [Google Scholar]
- Wang, X.; Gao, X.; Zhang, Z.; Cheng, L.; Ma, H.; Yang, W. Advances in modifications and high-temperature applications of silicon carbide ceramic matrix composites in aerospace: A focused review. J. Eur. Ceram. Soc. 2021, 41, 4671–4688. [Google Scholar] [CrossRef] [Scilit]
- Cramer, C.L.; Elliott, A.M.; Lara-Curzio, E.; Flores-Betancourt, A.; Lance, M.J.; Han, L.; Blacker, J.; Trofimov, A.A.; Wang, H.; Cakmak, E. Properties of SiC-Si made via binder jet 3D printing of SiC powder, carbon addition, and silicon melt infiltration. J. Am. Ceram. Soc. 2021, 104, 5467–5478. [Google Scholar] [CrossRef] [Scilit]
- Terrani, K.; Jolly, B.; Trammell, M. 3D printing of high-purity silicon carbide. J. Am. Ceram. Soc. 2020, 103, 1575–1581. [Google Scholar] [CrossRef] [Scilit]
- Zocca, A.; Lima, P.; Diener, S.; Katsikis, N.; Günster, J. Additive manufacturing of SiSiC by layerwise slurry deposition and binder jetting (LSD-print). J. Eur. Ceram. Soc. 2019, 39, 3527–3533. [Google Scholar] [CrossRef] [Scilit]
- Khan, F.; Arman, M.S.; Sanders, J.; Pasha, M.M.; Rahman, A.M.; Pei, Z.; Dong, T. Binder Jetting 3D Printing Utilizing Waste Algae Powder: A Feasibility Study. Intell. Sustain. Manuf. 2024, 1, 10016. [Google Scholar] [CrossRef] [Scilit]
- Mostafaei, A.; Elliott, A.M.; Barnes, J.E.; Li, F.; Tan, W.; Cramer, C.L.; Nandwana, P.; Chmielus, M. Binder jet 3D printing—Process parameters, materials, properties, modeling, and challenges. Prog. Mater. Sci. 2021, 119, 100707. [Google Scholar] [CrossRef] [Scilit]
- Miyanaji, H.; Zhang, S.; Lassell, A.; Zandinejad, A.; Yang, L. Process development of porcelain ceramic material with binder jetting process for dental applications. JOM 2016, 68, 831–841. [Google Scholar] [CrossRef] [Scilit]
- Gaytan, S.; Cadena, M.; Karim, H.; Delfin, D.; Lin, Y.; Espalin, D.; MacDonald, E.; Wicker, R. Fabrication of barium titanate by binder jetting additive manufacturing technology. Ceram. Int. 2015, 41, 6610–6619. [Google Scholar] [CrossRef] [Scilit]
- Crane, N.B. Impact of part thickness and drying conditions on saturation limits in binder jet additive manufacturing. Addit. Manuf. 2020, 33, 101127. [Google Scholar] [CrossRef] [Scilit]
- Mostafaei, A.; De Vecchis, P.R.; Kimes, K.A.; Elhassid, D.; Chmielus, M. Effect of binder saturation and drying time on microstructure and resulting properties of sinter-HIP binder-jet 3D-printed WC-Co composites. Addit. Manuf. 2021, 46, 102128. [Google Scholar] [CrossRef] [Scilit]
- Huang, S.; Wu, H.; Jiang, C.; Fu, X.; Liu, Y.; Zhang, J.; He, L.; Yang, P.; Deng, X.; Wu, S. Preparation of high-strength ZrO2 ceramics by binder jetting additive manufacturing and liquid glass infiltration. Ceram. Int. 2024, 50, 44175–44185. [Google Scholar] [CrossRef] [Scilit]
- Miyanaji, H.; Zhang, S.; Yang, L. A new physics-based model for equilibrium saturation determination in binder jetting additive manufacturing process. Int. J. Mach. Tools Manuf. 2018, 124, 1–11. [Google Scholar] [CrossRef] [Scilit]
- Lu, K.; Reynolds, W.T. 3DP process for fine mesh structure printing. Powder Technol. 2008, 187, 11–18. [Google Scholar] [CrossRef] [Scilit]
- Vaezi, M.; Chua, C.K. Effects of layer thickness and binder saturation level parameters on 3D printing process. Int. J. Adv. Manuf. Technol. 2011, 53, 275–284. [Google Scholar] [CrossRef] [Scilit]
- Enneti, R.K.; Prough, K.C. Effect of binder saturation and powder layer thickness on the green strength of the binder jet 3D printing (BJ3DP) WC-12% Co powders. Int. J. Refract. Met. Hard Mater. 2019, 84, 104991. [Google Scholar] [CrossRef] [Scilit]
- Fu, W.; Song, X.; Tian, R.; Lei, Y.; Long, W.; Zhong, S.; Feng, J. Wettability and joining of SiC by Sn-Ti: Microstructure and mechanical properties. J. Mater. Sci. Technol. 2020, 40, 15–23. [Google Scholar] [CrossRef] [Scilit]
- Pasha, M.M.; Arman, M.S.; Pei, Z.; Khan, F.; Sanders, J.; Kachur, S. Effects of Compaction Thickness on Density, Integrity, and Microstructure of Green Parts in Binder Jetting Additive Manufacturing of Silicon Carbide. J. Manuf. Mater. Process. 2025, 9, 136. [Google Scholar] [CrossRef] [Scilit]
- Pasha, M.M.; Arman, M.S.; Khan, F.; Pei, Z.; Kachur, S. Effects of Layer Thickness and Compaction Thickness on Green Part Density in Binder Jetting Additive Manufacturing of Silicon Carbide: Designed Experiments. J. Manuf. Mater. Process. 2024, 8, 148. [Google Scholar] [CrossRef] [Scilit]
- Leonard, R.D.; Edwards, D.J. Bayesian D-optimal screening experiments with partial replication. Comput. Stat. Data Anal. 2017, 115, 79–90. [Google Scholar] [CrossRef] [Scilit]
- Dorula, M.; Khademitab, M.; Jamalkhani, M.; Mostafaei, A. Location dependency of green density and dimension variation in binder jetted parts. Int. J. Adv. Manuf. Technol. 2024, 132, 2853–2861. [Google Scholar] [CrossRef] [Scilit]
- Hodder, K.J.; Nychka, J.A.; Chalaturnyk, R.J. Process limitations of 3D printing model rock. Prog. Addit. Manuf. 2018, 3, 173–182. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.