


Abstract
The solidification process is crucial for preparing high-performance superconductors and is strongly dependent on the characteristics of the starting powder, including particle size, morphology, and phase purity. This review concisely examines the study on four key superconductors: REBCO, Bi-2212, FeSeTe, and MgB2. In REBCO, additives such as CeO2, Pt, or BaO2 powder can refine the RE-211 phase. In Bi-2212, Pb doping stabilizes the high-Tc phase. For FeSeTe, doping with F or Co modifies phase separation and introduces Δκ pinning. Meanwhile, in MgB2, the incorporation of SiC nanoparticles powder generates effective pinning centers. Concurrently, processing conditions exert a decisive influence on the final microstructure, as demonstrated by the TSMG/TSIG route in REBCO, partial melting parameters for Bi-2212, specific cooling protocols and thermal treatments for FeSeTe, and optimized sintering and post-annealing processes for MgB2. Future research directions should prioritize fundamental understanding of phase separation mechanisms during powder processing, development of multi-component doping strategies for powder modification, and advancement of scalable powder processing routes for practical conductor architectures.
1. Introduction
For REBCO, Bi-2212, FeSeTe, and MgB2, the promising prospects for high-power applications are constrained by a common and critical issue. The solidification process is a main process crucial for preparing high-performance bulk and round wire. the prevalent occurrence of phase separation during solidification and heat treatment processes. This microstructural heterogeneity manifests in varied forms across different material systems, yet consistently leads to the degradation of macroscopic performance.
In REBCO melt-textured bulks, complex multi-element reactions and non-equilibrium solidification readily induce texture imperfections, inhomogeneous RE-211 distribution, and flux pinning center segregation [1,2,3,4]. These issues significantly compromise the current carrying capacity under high magnetic fields and the uniformity of properties. Similarly, in the isotropic bismuth-based Bi-2212 materials, incomplete phase transformation and porosity during melt processing not only reduce the critical current density (Jc) but also pose serious challenges to their stability in very high-field magnet applications [5,6,7]. For iron-based Fe(Se, Te) superconductors and the intermetallic compound MgB2, phase separation primarily manifests as compositional fluctuations (e.g., Se/Te) or deviation from stoichiometry of key elements (e.g., Mg), subsequently triggering secondary phase precipitation, weak intergranular coupling, and pore formation, which directly impair electrical connectivity and flux pinning effectiveness [8,9,10,11,12]. Therefore, despite the diversity of material systems, microstructural instability and chemical inhomogeneity resulting from solidification induced phase separation have emerged as a fundamental bottleneck limiting the enhancement of Jc, reproducibility of performance, and high-field applicability across various practical superconducting materials [13].
Beyond the common issue of phase separation, a unifying feature is identified across these superconductor families. Their entire processing chain begins with precursor powders. Take REBCO as an example. RE-123 and RE-211 powders are used [14]. In the case of Bi-2212, precursor powder is packed into silver tubes to produce round wires [5]. For iron-based superconductors, elemental Fe, Se, and Te powders are blended [9,15]. MgB2 relies on Mg and B powders for in situ synthesis [16,17]. In all cases, the journey to a high-performance superconductor starts with a powder. The initial characteristics of these powders are not incidental. These include particle size distribution, phase purity, morphology, agglomeration state, and dopant homogeneity. Instead, these characteristics serve as critical boundary conditions. They govern the thermodynamic and kinetic pathways of all subsequent transformations, including solidification and phase separation. Therefore, a profound understanding of powder precursors is established as the primary foundation. It dictates the final microstructure and, consequently, the ultimate superconducting performance.
Consequently, a profound comprehension and precise control of phase separation during solidification is pivotal for transitioning practical superconducting materials from laboratory research to engineering applications. This review systematically examines the effect of precursor powder on the solidification microstructure and superconducting properties of superconducting materials. It assesses the consequent effects on critical superconducting properties, including Jc, the transition temperature (Tc), and microstructural connectivity. Furthermore, the primary strategies for controlling this phenomenon are summarized. The objective is to provide a theoretical foundation and directional guidance for the process optimization and performance enhancement of these materials.
Existing reviews mainly summarize experimental results without critical comparison. By contrast, this review provides a systematic evaluation of competing doping strategies within each material system. At the end of each section, the advantages and limitations of different dopants are explicitly compared. Application-oriented recommendations (low-field vs. high-field) are then given based on these comparisons. Unlike previous reviews that focus on single material systems (e.g., REBCO alone or MgB2 alone), this review covers four superconductor families under a unified framework focusing on precursor powder characteristics. Thus, this review offers not just a literature summary but a practical guide for selecting powder modification strategies. In addition, these four systems are selected due to their practical relevance and the availability of sufficient literature on powder-processing relationships.
Direct comparison of Jc values across different studies is challenging due to variations in measurement conditions. In this review, Jc values are reported as given in the original sources and compared only within the same measurement conditions. No normalization is attempted to avoid introducing additional uncertainty.
2. Influence of Precursor Powder Characteristics on the Solidification Process and Performance of High-Tc Cuprate Superconductors
2.1. REBCO
Driven by their broad transformative potential, high-temperature superconductor (HTS) research constitutes a key research direction in materials science [4,18]. With their superior performance and enhanced efficiency, second-generation high-temperature superconductors (2G-HTS) hold great promise for critical applications ranging from energy transmission and medical imaging to advanced scientific instrumentation [1,19,20]. Since their discovery in 1986, REBCO (RE = rare earth element) high temperature superconducting bulks has attracted extensive attention due to their outstanding flux [20] trapping performance (>5 T) at liquid nitrogen temperature (77 K) [21]. The superconducting properties, particularly Jc and trapped field, are fundamentally dictated by the microstructural features developed during the solidification process.
In the fabrication process of REBCO bulk superconductors, the treatment of precursor powders represents the logical starting point that fundamentally determines the final sample performance, with a clear causal chain linking powder purity, particle size, distribution, final phase assemblage, flux pinning characteristics, and current carrying capacity. High-purity precursor powders are essential because subsequent heat treatments cannot eliminate impurity phases once introduced. For instance, in the preparation of Y2BaCuO5 powder by Antončík et al. [22], high-purity raw materials (99.99% Y2O3 and CuO) were employed, and repeated grinding and calcination were conducted between 1138 K and 1173 K. X ray diffraction analysis subsequently confirmed that a high-purity sample without detectable impurity phases was obtained, which established the foundation for accurate measurement of its thermodynamic properties. The Y-211 powder prepared by Antončík et al. showed uniform particle size (1–5 μm) and homogeneous elemental distribution, confirming its high purity (Figure 1) [22]. This confirms that high-purity starting powders can be achieved through solid-state reaction, which is a prerequisite for reliable measurement of thermodynamic properties and for achieving consistent superconducting performance.
Figure 1.
Morphology of the Y2BaCuO5 particles observed by SEM (a) and the associated elemental mappings acquired via EDS (b). Adapted from [22] with permission.
Once purity has been ensured, particle size becomes the most critical controllable variable. Extensive comparative studies have confirmed that refining the precursor powder particle size represents the most effective means of controlling the dimensions of the non-superconducting RE-211 second phase particles in the final microstructure. This process follows the principle of particle size inheritance: finer precursor powders result in smaller RE-211 particles retained within the RE-123 matrix, thereby introducing more pinning interfaces within the superconductor. For example, when ultra fine Gd-211 powder with an average particle size of only 0.1 μm was employed, submicron sized Gd-211 particle distributions were obtained in Gd-Ba-Cu-O bulk materials, which significantly enhanced Jc [23]. Additionally, when the infiltration growth process is adopted, powder treatment directly influences the uniformity of liquid phase infiltration and subsequent reactions, which consequently determines the distribution homogeneity of RE-211 particles in the final samples. This approach avoids the second phase free regions commonly observed in conventional melt textured samples, resulting in more uniform and denser microstructures [14,24].
However, powder refinement is not simply a matter of achieving the smallest possible particle size; it must be matched with the growth kinetics. In the top seeded melt growth process, excessively fine Y-211 powder tends to be pushed by the growth front rather than trapped near the seed crystal, which leads to the formation of macroscopic regions devoid of pinning centers beneath the seed and adversely affects the uniformity of performance [23]. In the infiltration growth process, by adjusting the cooling time, the Ostwald ripening of Y-211 particles can be effectively controlled, thereby avoiding particle coarsening that would otherwise occur with excessively long processing times and maintaining a uniform microstructure [25].
Single-grain REBCO bulk superconductors are typically fabricated via melt processes such as Top-Seeded Melt-Growth (TSMG) or Top-Seeded Infiltration and Growth (TSIG) [14,24,26]. Both methods are based on a peritectic reaction, wherein the REBa2Cu3O7-δ (RE-123) phase decomposes incongruently upon heating into solid RE2BaCuO5 (RE-211) particles and a Ba-Cu-O liquid phase. The subsequent slow cooling stage facilitates a seeded peritectic reaction between the RE-211 phase and the liquid phase [14,23]. This process results in the formation of a textured RE-123 single grain, thereby incorporating unreacted RE-211 particles, pores, and other non-superconducting phases as inclusions.
This chapter will systematically review the phase separation phenomena in REBCO materials during solidification. It will focus on two primary control strategies: compositional modification and process optimization, and will elaborate on how these microstructural features influence superconducting performance.
2.1.1. Compositional Design of Precursor Powders for Phase Refinement
The introduction of specific additives or the precise modification of the precursor composition represents one of the most direct and effective strategies for controlling the phase separation of the RE-211 secondary phase.
In the conventional TSMG process, the precursor powder typically consists of RE-123 mixed with an excess of RE-211, a common nominal ratio being 75:25 wt% [26]. The incorporation of the RE-211 phase serves multiple critical purposes: (i) to supply a sufficient source of RE elements for the peritectic growth of the RE-123 matrix, thereby promoting rapid crystal growth, (ii) to minimize the loss of the liquid phase during the high-temperature melting stage by reducing its mobility, and (iii) ultimately, to yield a dispersion of fine, non-superconducting RE-211 particles within the RE-123 matrix after solidification, which act as effective flux-pinning centers [27,28].
Other rare earth systems, such as GdBCO and SmBCO, exhibit higher Tc and Jc compared to YBCO. However, due to the similar atomic radii of rare earth and Ba atoms, these systems are prone to the formation of RE1+xBa2−xCu3Oy solid solutions, which significantly degrade their superconducting properties [28]. Table 1 summarizes the Jc values for REBCO bulks under various doping conditions [29,30,31,32,33,34]. Unless otherwise specified, all Jc values cited in this review were obtained from magnetization measurements using the Bean model.
Table 1.
Jc of REBCO bulks at 77 K under self-field for various doping conditions [29,30,31,32,33,34].
Adding 1–10 wt% BaO2 in GdBCO suppresses solid solution formation by providing additional oxygen and barium, thereby promoting pure RE-123 phase [1,29,30,31,34,35,36,37]. CeO2, Pt, and YGdNb-11411 suppress Ostwald ripening of RE-211 particles, leading to refined and uniform distributions [31,32,33,34,38,39,40,41].
Figure 2 directly compares the performance of the REBCO samples listed in Table 1, highlighting a crucial distinction in how different compositional modifications affect the superconductor. Chemical additives (e.g., BaO2, Pt, CeO2) effectively enhance the self-field Jc. However, they often result in a strong magnetic field dependence, leading to a rapid decline at higher fields. This is evident in the similar, steeper degradation curves of samples like GdBCO (BaO2 + Pt) [30] and YBCO (CeO2) [31]. In contrast, introducing designed secondary phase nanoparticles (e.g., YGdNb-11411) serves a different primary function: to directly and robustly enhance flux-pinning capability. The GdBCO sample with YGdNb-11411 nanoparticles demonstrates this principle clearly. It not only achieves the highest self-field Jc but, more importantly, exhibits the most gradual decay with increasing field. This superior performance across the entire 0–5 T range signifies the creation of a more effective pinning. Therefore, this figure underscores a strategic guideline for performance optimization: additives are essential for refining the primary microstructure and boosting zero-field performance, but the incorporation of tailored secondary phase nanoparticles is critical for building strong, field-independent pinning centers that ensure high current capacity under practical magnetic operating conditions.
Figure 2.
Magnetic field dependence of the Jc at 77 K for the doped REBCO bulk superconductors listed in Table 1. The data for black, red, blue, green, purple, and orange curves are from Refs. [29,30,31,32,33,34].
2.1.2. Processing Solidified Microstructures from Engineered Powders
The solidification pathway plays a critical role in determining the spatial distribution of the RE-211 phase in REBCO, influencing its phase separation at both the macro- and micro-scale. Figure 3a,b show that the growth of the RE-123 phase exhibits a strong anisotropy between its a-b plane and c-axis, which consequently determines the final distribution and dimensions of RE-211 inclusions within the single-domain matrix [41]. This anisotropy explains why RE-211 inclusions tend to align along specific crystallographic directions, which directly affects the spatial distribution of flux pinning centers.
Figure 3.
Growth rates of YBCO along (a) the a/b-axis and (b) the c-axis as a function of undercooling ΔT for different Y-211 contents. Reprinted with permission from [41]. Licensed under CC BY 4.0.
The growth velocity of the RE-123 phase and the grain size of the RE-211 particles determine whether the RE-211 particles are trapped within the matrix or is pushed by the advancing growth front [42]. A larger undercooling promotes a higher growth rate, which favors the trapping of finer particles, leading to a uniform distribution of refined RE-211. In contrast, a smaller undercooling can result in particle pushing, causing macroscopic segregation [3,41]. In the TSMG process, the final distribution of RE-211 particles and the formation of microstructural defects in REBCO bulks are collectively determined by the growth mode (isothermal or undercooling) and the characteristics of the precursor powder. An optimized isothermal growth process utilizing a specifically formulated precursor powder has been shown to yield a superior spatial distribution of refined RE-211 inclusions [43].
Table 2 [14,24,44] shows a comparative summary of the TSMG and TSIG processes for REBCO bulk superconductors, detailing precursor materials, in situ reactions, and the results. In the TSIG process, the liquid phase source is comprised of a mixture of Y2O3, CuO, and BaCuO2 in a specific molar ratio.
Table 2.
Comparison of the TSMG and TSIG Processing Techniques [14,24,44].
A comparative analysis of the two processing techniques reveals that the TSIG route is fundamentally superior for microstructural control [14,24,45,46]. In the conventional TSMG process, peritectic decomposition of the RE-123 phase generates gaseous species. This leads to pore formation and concurrently precipitates RE-211 particles. These newly formed RE-211 particles are highly susceptible to coarsening via Ostwald ripening within the liquid matrix. They also become heterogeneously distributed due to liquid phase migration. Consequently, this results in a microstructure characterized by coarse and inhomogeneous RE-211 inclusions, as visually contrasted in Figure 4a,b. In contrast, the TSIG technique entirely circumvent the peritectic decomposition of the RE-123 phase. This process utilizes a pre-sintered preform of fine, precursor RE-211 powder as a stationary solid skeleton, which is infiltrated by a liquid phase source. Since the RE-211 particles are immobilized within this rigid framework, their coarsening is effectively suppressed, and their initial fine size and uniform spatial distribution are preserved throughout the growth process. This yields the refined, dense, and homogeneous dispersion of RE-211 particles evident in Figure 4c,d. This difference directly explains why TSIG samples exhibit more uniform Jc across different spatial positions (Figure 5), as the homogeneous RE-211 distribution provides consistent pinning throughout the sample volume.
Figure 4.
Optical micrographs of YBCO samples fabricated by (a,b) TSMG and (c,d) TSIG. (b) and (d) are higher-magnification views of the regions in (a) and (c), respectively [24] (CC BY 4.0).
Figure 5.
Magnetic field dependence of Jc at 77 K for YBCO bulks fabricated by TSMG and TSIG. Suffixes -1, -2, -3 indicate different locations within the same bulk. Data are extracted from [14] (CC BY 3.0).
The superior microstructural homogeneity achieved by TSIG is also reflected in the uniformity of the superconducting properties [14]. Figure 5 compares the magnetic field dependence of Jc at 77 K for YBCO bulks fabricated by TSMG and TSIG. TSMG samples show higher but position-dependent Jc, while TSIG samples exhibit lower but more uniform Jc, demonstrating the improved microstructural homogeneity achieved by TSIG. This indicates that TSIG offers better microstructural uniformity at the expense of peak Jc. For applications requiring consistent performance across large volumes (e.g., trapped field magnets), TSIG is therefore preferred despite its lower peak Jc.
Additionally, the content and distribution of RE-211 inclusions in the RE-123 matrix can be optimized by adjusting key processing parameters, specifically, infiltration temperature, time, and liquid phase content in the precursor [24,44]. This approach effectively addresses the issue of excessive RE-211 (>40%) that impaired the performance of early TSIG samples [14]. The development of the two-step BA-TSIG process, which separates the infiltration and grain growth stages, has led to a significant improvement in the precision of phase separation control and the overall reliability of the process [47]. The fabrication of REBCO bulk superconductors inherently relies on the quality of precursor powders. In practice, RE-123 and RE-211 powders are most commonly prepared by solid-state reaction. The particle size, purity, and stoichiometry of these starting powders are known to have a direct impact on the subsequent melt growth process. The critical role of precursor characteristics is further exemplified in Figure 6, which contrasts the outcomes of using coarse versus fine Y-211 powders [27]. The finer Toshima powder (Figure 6b,d) not only promotes a larger single-grain growth area but also yields a microstructure with markedly refined and homogeneously dispersed Y-211 particles, compared to the coarser Nexans powder (Figure 6a,c). This demonstrates that controlling the initial powder size is as important as optimizing thermal processing parameters, because finer precursor particles directly translate into finer secondary phase inclusions, which serve as more effective flux pinning centers.
Figure 6.
Influence of Y-211 precursor powder size on single-grain growth morphology. (a,b) Top surface views and (c,d) optical micrographs of YBCO grains from (a,c) coarse Nexans and (b,d) fine Toshima powders. Image from [27] under the terms of the CC BY 3.0.
RE-211 particles serve as the primary natural pinning centers in REBCO. Their pinning mechanism originates from defects at the RE-211/RE-123 interface due to lattice mismatch [48,49]. Optimizing RE-211 particle size and distribution increases the effective pinning site density and improves Jc [22]. This can be achieved by optimizing solidification conditions [25,44,50] or adding second phases such as CeO2, Pt, or Y2Ba4CuNbOy [28,34,51,52].
However, in REBCO superconductors, the formation of a solid solution is detrimental, as it disrupts phase homogeneity, resulting in a severe degradation of both Tc and Jc [34,44]. In addition, an inhomogeneous macroscopic distribution of the RE-211 phase can lead to uneven current transport paths and the formation of local weak links, which consequently degrades the overall trapped field performance [53,54,55,56]. In response to these challenges, a range of integrated strategies has been developed to further optimize the growth uniformity of single-domain REBCO. These strategies include the optimization of seeded growth techniques, precise control over the composition and distribution of the RE-211 phase in precursor powders, and the implementation of buffer layers [1,14,24,44]. Complementing the compositional and process engineering approaches discussed above, these methods are designed to suppress macro-segregation and structural defects on a larger scale. Collectively, they provide a more comprehensive technological pathway for achieving reliable fabrication of high-performance REBCO superconductors.
Of the doping strategies compared above, two distinct functions are identified. For CeO2 and Pt, the primary role is to refine the RE-211 particle size. Thereby, the zero-field Jc is enhanced. For YGdNb-11411 nanoparticles, by contrast, additional pinning centers are directly introduced. As a result, a higher Jc is maintained over a wide magnetic field range. Based on this distinction, the following strategy recommendations are made. For low-field applications, such as magnetic shielding, Pt or CeO2 doping is preferred. For high-field applications, such as rotating machinery, YGdNb-11411 nanoparticle doping is more advantageous. Unlike REBCO, which relies on melt-texturing, Bi-2212 is processed via the powder-in-tube route. Its phase separation behavior and doping strategies are discussed next.
2.2. Bi-2212
Bi-2212, as a representative high-temperature superconducting cuprate, is a promising candidate for high-field magnet applications due to its excellent processability, such as the ease of fabricating isotropic round wires, and its potential for high Jc under high magnetic fields. The properties of precursor powders and their processing conditions are critical factors that determine the final performance of its superconducting wires and coils. The stoichiometry and phase assemblage of the powder fundamentally control the reaction pathway during subsequent heat treatments. While precursor powders with a nominal “521” composition (Bi2.17Sr1.94Ca0.89Cu2Ox) are widely utilized, the fabrication route, whether co-precipitation or spray combustion, can lead to significant differences in phase purity and distribution, which directly impacts the wire performance [57,58]. The uniformity of the calcination process is largely governed by powder packing and heating protocols. It has been demonstrated that high heating rates or densely packed powders can trap CO2 released during carbonate decomposition. This entrapment creates a locally reduced oxygen partial pressure, which lowers the melting point of Bi-oxide phases and induces premature melting at temperatures as low as 740 °C. Such melting is detrimental as it promotes phase separation, grain coarsening, and overall precursor inhomogeneity, ultimately degrading Jc [59]. To preserve homogeneity and avoid the formation of this transient melt, a loosely packed powder bed combined with moderate heating rates is required to ensure adequate gas exchange.
Furthermore, the calcination temperature itself dictates the phase assemblage and morphology of the precursor powder. Low-temperature calcination (e.g., 710 °C) yields a homogeneous mixture of fine, intermediate phases. These phases are considered favorable as they lead to a more uniform peritectic decomposition during the final partial melt processing, thereby supporting a high Jc. In contrast, high-temperature calcination promotes the formation of large, plate-like grains (such as the 2201 phase), which contribute to compositional inhomogeneity on a larger scale and are correlated with reduced current-carrying capacity [59].
However, similar to many complex oxides, Bi-2212 is highly susceptible to phase separation during solidification from the high-temperature melt or subsequent heat treatment, resulting in a complex microstructure that influences its superconducting properties. This section systematically discusses the control of phase separation in Bi-2212 and its correlation with performance from two perspectives: compositional doping and processing techniques.
2.2.1. Powder Doping Strategies for Microstructural Optimization
In the Bi-2212 system, elemental doping serves as an important means to regulate phase separation behavior during solidification and ultimately tailor the superconducting properties. The primary objective lies in optimizing the microstructure to enhance key performance parameters such as the Jc and Tc. Studies indicate that rational selection of doping elements combined with precise control of processing conditions can significantly improve performance. For instance, the addition of Ag under low oxygen partial pressure promotes c-axis texturing and suppresses pore formation, which is beneficial for increasing Jc [60]. Partial substitution of Ca2+ by an appropriate amount of Na+ (e.g., x = 0.10) can elevate Jc to 1.35 × 10⁵ A/cm2 at 10 K, while at x = 0.075, Tc is optimized to approximately 93.3 K. This enhancement is primarily attributed to increased grain size, improved texture, and a reduction in secondary Bi-2201 phase content [61]. Nane et al. confirmed that Na doping (x = 0.075) can raise Jc in textured ceramics to 1.38 × 10⁵ A/cm2 at 10 K [62].
As shown in Figure 7 [63], when Na doping is low (x ≤ 0.02), the sample is mainly the Bi-2212 phase with good texture. However, when doping increases to 0.05 at% or higher, clear peaks of the non-superconducting Bi-2201 phase appear (▽). This shows that too much Na causes the Bi-2212 phase to break down during sintering, leading to harmful phase separation. This separation reduces the superconducting phase, breaks grain connections, and can weaken the benefits of low doping. Therefore, Na doping works best within a certain range, enough to improve pinning, but not so much that it causes bad phase separation.
Figure 7.
XRD patterns of SPS-sintered Bi-2212 bulks with different Na doping contents (x = 0, 0.02, 0.05, 0.10 at%). Adapted from [63] (CC BY 4.0).
However, doping may also lead to detrimental phase separation or introduce impurity phases that degrade performance. For example, Ag can react with the oxide melt during partial melting to form Ag-rich Cu dendritic phases (such as Ag0.98Cu0.02 and Ag0.24Cu0.76) [64]. These dendritic phases may disrupt the connectivity between Bi-2212 grains, constituting a microstructural factor that limits Jc. Excessive partial substitution of Cu2+ by Ti4+ introduces impurity phases such as SrTiO3 and alters lattice parameters, subsequently causing significant reductions in Jc and Tc [65]. The origin of these performance variations lies in the profound influence of Ag doping on the phase equilibria, solidification pathway, and microstructural evolution within the Bi-2212 system. The addition of Ag markedly lowers the primary crystallization temperature of the 2212 phase and modifies the type and stability of equilibrium solid phases within the melt (e.g., promoting the formation of (11) and (21) phases while suppressing the stability of the (9115) phase) [66]. Concurrently, Ag dissolves into the liquid phase, lowering the system’s melting point and reducing the Cu content in the melt [67]. These changes subsequently affect texture formation, densification, and intergranular connectivity, ultimately optimizing the superconducting properties.
Pb doping, when its content exceeds a certain threshold (e.g., x ≥ 0.4), induces a distinct phase separation characterized by a two-phase lamellar microstructure. The interfaces in this structure are oriented perpendicular to the CuO2 planes and can effectively suppress thermally activated flux flow, leading to a notable enhancement of both Jc and the irreversibility field Hirr [68]. Pb doping has long been recognized for its favorable improvements in the Bi-2212 phase [69]. By substituting Bi3+ with Pb2+, it increases the formal Cu valency and thus the number of hole charge carriers [70], leading to a sizable enhancement in Jc under magnetic field at an optimal Pb content of x = 0.16 [71]. Simultaneously, Pb doping significantly reduces the melting point of the Bi-2212 phase and alters its decomposition path upon melting, causing it to decompose into a liquid phase and (Sr, Ca)CuO2 in air [72]. Microstructural analyses of high-performance Bi-2212 conductors further reveal that after melt processing, Bi-2212 grains commonly exhibit a composition characterized by Bi excess and alkaline-earth deficiency, along with numerous Bi-2201 intergrowth structures and amorphous/nanocrystalline layers. These microstructural features are closely linked to the conductor geometry (e.g., round wires) and their specific melt-processing history [73].
Figure 8 presents the Scanning Electron Microscopy (SEM) images of the surface morphologies. Platelet-like grains, with sizes around 10 μm, which dependent on the synthesis and sintering procedures, are observed in the reference sample. The influence of doping on morphology is found to follow two opposite trends depending on the dopant element. Moderate doping with Zn or Ti is associated with an increase in platelet size. At higher Ti concentrations, as in sample Ti10, a notably compact structure is formed, characterized by merged layers and intersected by only a few tubular cavities. The surfaces of the platelets appear clean and smooth, with neat borders. In contrast, samples doped with Y and Nd exhibit smaller flat flakes, approximately 2 µm in size. The flake size is observed to decrease with increasing dopant content, approaching a granular aspect ratio in sample Y05. This morphological variation indicates that different dopants distinctly alter the grain growth behavior of Bi-2212, with Zn/Ti promoting coarsening and Y/Nd promoting refinement.
Figure 8.
SEM micrographs demonstrating the distinct morphological evolution of Bi-2212 grains induced by different dopant elements. Reproduced from [74] under the terms of the Creative Commons Attribution license.
The preceding discussion elucidates, from a mechanistic perspective, the influence of various elemental dopants on the phase separation and properties of Bi-2212. To provide a more direct comparison of the quantitative enhancement in superconducting current-carrying capability achieved by different doping strategies, Table 3 summarizes the self-field Jc data for representative doped Bi-2212 samples. As can be seen, appropriate doping with Na or K significantly enhances Jc, particularly at low temperatures (10 K or 4.2 K), where the improvement can reach up to an order of magnitude. This offers clear experimental evidence for optimizing Bi-2212 performance through compositional design.
Table 3.
Self-field Jc of doped Bi-2212 at 4.2 K and 10 K, respectively.
Beyond conventional dopants, the intrinsic composition of the precursor powder itself offers another route for performance optimization. Xu et al. recently demonstrated that increasing the Sr content in Bi-2212 powder from 1.34 to 2.13 per formula unit enhances flux pinning, raising Tc from 75.5 K to 80.4 K and Hk at 20 K from 3.5 T to 6.7 T [77]. In summary, the precise doping with elements such as Ag, Na, and Pb enables the thermodynamic and kinetic regulation of the phase equilibria and solidification pathway in the Bi-2212 system, thereby optimizing its microstructure and superconducting properties. In addition to compositional design, processing parameters are also recognized as exerting a decisive influence on phase separation behavior, which will be discussed in detail in the following section.
2.2.2. Thermal Processing of Bi-2212 Powders for Enhanced Connectivity
The fabrication of Bi-2212 round wires is typically carried out by the powder-in-tube (PIT) method, in which Bi-2212 precursor powder is packed into silver tubes and subsequently drawn into multifilamentary wires. The quality of the starting powder, including its phase purity, particle size, and flowability, is considered to have a direct influence on the fill factor, filament uniformity, and ultimately the critical current density of the final wire [78]. Processing parameters critically govern phase separation and superconducting properties in Bi-2212. For powder-in-tube (PIT) multifilamentary round wires, atmospheric pressure (1 bar) heat treatment leads to poor connectivity from bubbles and pores formed during melting, severely limiting Jc. Conversely, applying an overpressure heat treatment (100 bar) effectively suppresses bubble formation and enhances Bi-2212 phase densification. This leads to an eightfold increase in the engineering current density (Je) and successfully generates an additional field of 2.6 T within a 31.2 T background field, demonstrating its potential for high-field magnet applications [5]. Subsequent studies have further clarified how precursor powder characteristics affect the overpressure heat treatment window and subsequent wire processing. Crucial to the heat treatment window is powder quality. Wires made from higher-quality Engi-Mat powder, for instance, exhibit a wider processing window (ΔTmax ∼ 10 °C) than those made from older Nexans powder [79,80]. Also influenced by powder quality are effective filament diameter and anisotropy, as well as strain tolerance and current uniformity [81]. Of equal importance is powder reactivity, which affects filament bridging and hysteretic losses [82]. Furthermore, Jc degradation under rolling deformation saturates beyond a thickness reduction of 15–20%, a finding with clear implications for powder selection in cable applications [83]. Further research by Nachtrab et al. on optimizing Bi-2212/Ag wire performance via a single-stack multifilamentary process revealed that increasing the superconductor fill factor (to 35–40%) and reducing the single filament diameter (below 18 μm) significantly enhance both Jc and n value, while the influence of filament spacing (s/d) is relatively minor [84]. This provides crucial guidance for wire design aimed at MRI applications.
Oxygen partial pressure and temperature schedule during heat treatment also profoundly affect phase composition and microstructure. Comparative studies by Holesinger et al. on melt processing under oxygen and argon atmospheres showed that melting in argon followed by annealing in oxygen yields a more uniform microstructure compared to melting and annealing entirely in oxygen. This process forms dominant Bi2Sr3−xCaxO7 and Cu2O/CuO eutectic structures, with the final annealing step recovering the 2212 phase with a relatively high-Tc of approximately 88–89 K [84]. In-depth research by Marinkovic et al. demonstrated that within the temperature range of 865–900 °C, the peritectic melting of Bi-2212 exhibits two distinct regimes. Below 890 °C, incomplete melting occurs, forming a small amount of fine second phases such as (Sr, Ca)14Cu24O41 and Bi5Sr11Ca5O4. However, insufficient oxygen uptake results in a low superconducting volume fraction. Above 890 °C, complete melting takes place. Although this generates a larger quantity of coarse second phases, sufficient oxygen absorption significantly increases the proportion of the Bi-2212 phase, consequently achieving a Jc as high as 1000 A/cm2 at 77 K in self-field [85]. Investigations of crystal growth in the Bi-Sr-Ca-Cu-O system by Kameneva et al. revealed that slow cooling after high temperature (≥1000 °C) homogenization leads to the quantitative formation of a red eutectic structure composed of a Bi16(Sr, Ca)14O38 matrix with Cu2O rod-like precipitates. The formation of this structure indicates the presence of numerous 2201-type stacking faults within the grown 2212 crystals, revealing a connection between the solidification path and crystal defects [86]. Finally, research by Imayev et al. showed that applying a quasi-hydrostatic pressure of about 10 MPa can raise the melting point of Bi-2212 by approximately 60 °C and alter its decomposition products. At atmospheric pressure, a Cu-poor (Sr, Ca)CuO2 phase forms, whereas under pressure, a Cu-rich (Sr, Ca)14Cu24O41 phase is produced. This indicates that pressure enhances the thermal stability of the material by suppressing structural instability, likely through the locking of apical oxygen within the lattice [87].
In summary, a range of strategies has been developed to optimize the phase evolution and superconducting performance of Bi-2212. As discussed throughout this section, the introduction of dopants such as Ag, Na, and Pb has been widely employed to regulate phase equilibria and refine the resulting microstructure [60,61,62,63,64,66,67,68,69,70,71,72]. Concurrently, careful optimization of heat treatment parameters, including atmosphere control, overpressure processing, and precise temperature scheduling, has been demonstrated to be critical for enhancing densification and intergranular connectivity [5,78,84,85,86]. For instance, doping with Ag or TiO2, combined with optimized thermal processing, has been shown to effectively refine the microstructure, reduce porosity, and enhance the critical current density in high-field applications [5,65,87,88]. These complementary approaches, rooted in both compositional design and process engineering, form the foundation for achieving reliable, high-performance Bi-2212 conductors suitable for demanding magnet applications. Of the three doping strategies compared (Na, Pb, and Ag), distinct advantages and limitations are observed. For Na doping, the highest Tc enhancement (up to 93.3 K) is achieved. However, when the doping level exceeds x = 0.02, the detrimental Bi-2201 phase is induced. For Pb doping (x ≥ 0.4), a two-phase lamellar microstructure is formed. Thereby, thermally activated flux flow is effectively suppressed. This makes Pb doping suitable for high-field applications. For Ag doping, Jc is primarily enhanced through improved texture and densification. However, Ag-Cu dendritic phases may form, which damage grain connectivity. Based on this comparison, the following recommendations are made. For high-field magnet applications, Pb doping is preferred. For ceramic materials requiring a high-Tc, Na doping is more suitable. Compared with REBCO, Bi-2212 exhibits a fundamentally different phase separation behavior. In REBCO, the key issue is controlling RE-211 particle size and distribution. In Bi-2212, the main challenge is suppressing the formation of the non-superconducting Bi-2201 phase and reducing porosity during melt processing. This difference explains why doping strategies in Bi-2212 focus on stabilizing the high-Tc phase (e.g., Pb doping) or enhancing texturing (e.g., Ag doping), rather than refining secondary phase particles. Importantly, the overpressure heat treatment (100 bar) has been shown to suppress bubble formation and enhance densification, leading to an eightfold increase in engineering current density. This strategy is unique to Bi-2212 and has no direct counterpart in REBCO processing. Beyond cuprate superconductors, iron-chalcogenide FeSeTe offers a distinctly different phase separation mechanism, as examined in the following section.
3. Powder Processing of FeSeTe: From Elemental Mixtures to Superconducting Phases
The emergence of iron-based superconductors (IBSCs) has stimulated extensive investigation into their synthesis, motivated by their exceptional upper critical fields and high critical current densities [89,90,91,92]. Owing to its structural simplicity, high upper critical field, and low toxicity, the Fe(Se, Te) system, a prominent member of the “11” family, is considered a promising system for applied studies [93,94,95,96,97,98]. Bulk solidified Fe(Se, Te) materials have been the subject of extensive research as promising candidates for practical applications.
Due to the presence of a miscibility gap in the FeSeTe system [99,100], macroscopic phase separation readily occurs during solidification from the high-temperature melt, resulting in the formation of Se-rich and Te-rich phase regions [10,101,102].
The superconducting performance is ultimately dictated by microstructural architecture. The morphology of phase-separated regions and the degree of chemical homogeneity critically determine flux pinning efficacy and current carrying capacity across grain boundaries [8,9,101,102]. Furthermore, the solidification pathway and subsequent thermal processing significantly influence the precipitation behavior of secondary phases (e.g., the hexagonal δ-FeSe or Fe7Se8 phase), the elemental distribution, and the concentration of interstitial iron, which serve as pivotal parameters for optimizing Jc and pinning performance [8,100,103,104,105,106].
This chapter provides a systematic review of the phase separation phenomena in FeSeTe materials during solidification. It focuses on the strategies for its control through composition design and processing parameters, and analyzes the influence of the resulting microstructures on superconducting properties.
3.1. Powder Modification via Doping and Stoichiometry Control
FeSeTe polycrystalline materials are typically prepared by solid-state reaction using elemental Fe, Se, and Te powders as starting materials. The mixing and ball milling conditions, including milling time, speed, and medium, are known to influence the homogeneity of the elemental distribution. This homogeneity, in turn, affects the formation of the superconducting phase and the extent of phase separation during subsequent sintering [8,102]. The phase composition and distribution in FeSeTe materials can be precisely manipulated through adjustments in stoichiometry or the introduction of dopant elements, thereby enabling subsequent optimization of their superconducting properties.
The Se/Te ratio serves as a critical factor in determining the phase composition of the FeSe1−xTex system. An optimal ratio near x = 0.5 facilitates a homogeneous microstructure dominated by the superconducting Fe(Se, Te) phase and minimizes the formation of detrimental secondary phases [103,107,108].
The incorporation of a new element or compound is an effective approach for tailoring the microstructure of FeSeTe. By introducing a new element or specific compounds, it is possible to optimize grain structure, suppress the formation of detrimental phases, and introduce effective flux pinning centers. Consequently, the superconducting properties, particularly Jc, can be significantly enhanced.
The effects of transition metal doping on the superconducting properties of the Fe(Se, Te) system have been extensively investigated. In a systematic study on Fe0.95TM0.05Se0.5Te0.5, for instance, Zhang et al. reported that doping with Mn or Co only slightly modifies Tc, even leading to a minor enhancement [109]. In contrast, the introduction of Ni or Cu completely suppresses superconductivity. Gawryluk et al. systematically evaluated the doping behavior of multiple elements, including Co, Ni, Cu, Mn, Zn, Mo, Cd, and In, in FeTe1−xSex single crystals. Their results indicated that only Co, Ni, and Cu can effectively substitute for Fe sites in the lattice [110], whereas the other elements predominantly formed secondary-phase inclusions, consequently modifying the matrix composition and affecting Tc. Building on this, the study by Liu et al. further demonstrates that trace Co doping (<1 at %) in FeSe0.4Te0.6 single crystals successfully incorporates Co at the Fe sites, resulting in a slight contraction of the lattice parameters and a significant enhancement of Jc under high magnetic fields [111].
In addition to transition metal dopants, non-metal element doping has proven to be highly effective in tailoring the microstructure and superconducting performance. A prominent example is fluorine doped Fe(Se, Te), where F doping is found to induce a distinctive dual-oscillation effect [9]. Firstly, the microstructure of the undoped sample is typical of phase separation during melting. Remarkably, F doping triggers a dramatic change, leading to a pearlite-like morphology, defined by the periodic alternation of the β-Fe(Se, Te) and δ-Fe(Se, Te) phases. This self-organization is a direct consequence of altered phase formation kinetics induced by the fluorine. Secondly, a chemical compositional oscillation occurs due to inhomogeneous distribution of Se and Te within the β-phase. These dual oscillations collectively change the primary flux pinning mechanism from surface pinning to Δκ pinning, thereby promoting a substantial improvement in both Jc and Hc2.
Furthermore, the addition of FeF2 transforms the phase-separation morphology from typically irregular, flower-like patterns into a macroscopically ordered structure characterized by submillimeter-scale striations aligned along the c-axis [10]. As shown in Figure 9, the backscattered electron images clearly illustrate this morphological transition: the FeF2-free sample exhibits a typical flower-like Se-rich phase distribution (Figure 9a), while the FeF2-added sample displays a regular, striated morphology with alternating Se-rich and Te-rich phases (Figure 9b). Comprising the well-defined phases FeSe0.6Te0.4 and FeSe0.4Te0.6, this configuration enhances phase purity, leading to the induction of a Δκ pinning mechanism. Consequently, a superior superconducting performance is achieved, characterized by simultaneous enhancements in Tc, Hc2, and Jc.
Figure 9.
BSE images of the (a) FeF2-Free sample and (b) FeF2-added sample, all polished along the c-axis. From Ref. [10] under CC BY-NC-ND 4.0.
The significant improvement in current carrying capacity is directly evidenced by the magnetic field dependence of Jc. As shown in Figure 10, at 4.2 K, the FeF2-added sample with macroscopically ordered phase separation exhibits substantially higher Jc values than its FeF2-free counterpart across the entire field range, especially under high magnetic fields (e.g., 7 T). This demonstrates that the ordered phase separation structure effectively enhances flux pinning and mitigates the suppression of Jc by magnetic fields.
Figure 10.
Magnetic field dependence of Jc at 4.2 K for (a) FeF2-free and (b) FeF2-added Fe(Se, Te) samples. Data in panels (a,b) are replotted from panels (c,d) of Figure 6 in Ref. [10], CC BY-NC-ND 4.0.
The underlying change in flux pinning mechanism is revealed by analyzing the normalized pinning force. As shown in Figure 11, the scaling behavior of the pinning force (fp) as a function of reduced field (H/Hirr) differs significantly between the two types of samples. For the common phase separated sample (Figure 11a), the dominant pinning mechanism shifts from point pinning to surface pinning as temperature increases. In contrast, the sample with macroscopically ordered phase separation (Figure 11b) exhibits the emergence of Δκ pinning at low temperatures, and the transition to surface pinning is notably delayed. This indicates that the regular, stoichiometry-defined phase boundaries in the ordered structure create a more effective and thermally stable pinning landscape.
Figure 11.
Normalized pinning force fp as a function of reduced field H/Hirr for (a) FeF2-free and (b) FeF2-added Fe(Se, Te) samples at various temperatures. Data in panels (a,b) are replotted from panels (e,f) of Figure 6 in Ref. [10], CC BY-NC-ND 4.0.
A co-doping strategy employing Ag and O was developed by Liu et al. to concurrently improve intergranular connectivity and flux pinning in Fe(Se, Te) polycrystals [112]. Ag segregated at grain boundaries to enhance current transport, while oxygen from SeO2 mitigated the detrimental interstitial Fe by forming Fe2O3 precipitates that acted as effective pinning centers. This approach resulted in an approximate 4.7-fold increase in Jc at 8 T and 5 K for the 0.05 Ag/O Co-doped sample. Similarly, Chen et al. reported that trace Sn doping in FeSe0.5Te0.5 bulks promoted the formation of a near-stoichiometric superconducting phase and suppressed secondary phases, leading to improved microstructural homogeneity [105]. This structural refinement resulted in a self-field Jc of 9 × 10³ A/cm2 at 4.3 K and a retained Jc of 4 × 10² A/cm2 at 5 T, indicating a significant enhancement of in-field current transport. To provide a more intuitive comparison of the impact of different doping strategies on the current carrying performance of FeSeTe superconductors, Figure 12 summarizes the Jc-H curve for representative doped samples at 5 K. The curves clearly illustrate that the Co-doped [111] sample exhibits superior field dependence performance, maintaining the highest Jc values across the entire field range (0–5 T). In contrast, the other doped samples (e.g., F-doped [9,10], Cl-doped [15], and Ag/O co-doped [112]) show varying degrees of field suppression. While their Jc degradation trends share a broadly similar downward trajectory, differences in absolute Jc values are evident, particularly at intermediate and high fields. This direct comparison confirms the unique efficacy of Co doping in creating flux-pinning centers and demonstrates that the other dopants, despite showing some improvement, are less effective than Co in mitigating field induced suppression of Jc.
Figure 12.
Comparison of the Jc for various doping strategies in FeSeTe superconductors. The data for red, black, purple, blue, and green curves are from Refs. [9], [10], [15], [111], and [112], respectively.
Collectively, the doping strategies discussed above operate through a common underlying principle: the induction of structural and compositional modulations within the Fe(Se, Te) matrix. As demonstrated with elements such as F, Sn, Co, or Cl, these modulations effectively alter the flux pinning landscape, introducing novel pinning mechanisms (e.g., Δκ pinning) or refining the existing pinning architecture [9,10,15,111,112]. Consequently, a substantial enhancement in high-field performance, particularly in terms of Jc, has been consistently achieved across various doping systems. Figure 12 provides a direct comparison of the influence of different doping strategies on the magnetic field dependence of Jc at 5 K. The data clearly illustrate that while all modifications enhance performance to some degree, Co doping exhibits a superior ability to mitigate field-induced suppression of Jc across the entire measured field range. To allow a more systematic evaluation of the performance differences among the doping systems, Table 4 summarizes the Jc values of representative FeSeTe polycrystalline samples at self-field and at 5 T, covering both undoped and chemically doped cases. These data offer a quantitative basis for comparing the effectiveness of the various doping approaches.
Table 4.
Summary of Jc values at self-field and 5 T for undoped and doped FeSeTe polycrystalline samples from literature [9,10,15,105,111,112].
Beyond compositional design, the physical processing of the precursor powder itself plays a critical role in determining the final microstructure and superconducting properties. In the preparation of Fe(Se, Te) superconductors, the precise handling of precursor powders is established as a fundamental prerequisite for achieving optimal final performance. Initially, the weighing and mixing of high-purity elemental powders (Fe, Se, Te) must be conducted within a high-purity inert atmosphere (e.g., an argon-filled glove box) to rigorously avoid oxidation or hydration. Even minor oxygen or moisture contamination can introduce magnetic impurities such as Fe2O3, which are detrimental to superconductivity [113,114,115]. Mechanical processing of the powder mixture significantly influences the kinetics of subsequent reactions. The application of high-energy ball milling (HEBM) has been demonstrated to directly form Fe-Se-Te ternary compound precursors via mechanical alloying, while concurrently refining particle size and shortening atomic diffusion paths. This approach fundamentally mitigates volume expansion and porosity caused by the volatilization of liquid Se and Te during conventional sintering. Consequently, the density of the sintered body is substantially increased from 2.29 g/cm3 to 5.61 g/cm3, enabling the fabrication of high-performance samples at reduced sintering temperatures and durations [116].
3.2. Sintering and Annealing: Transforming FeSeTe Powders into High-Performance Bulks
The solidification pathway, which encompasses cooling rate, thermal gradient, and post-processing heat treatment, exerts a decisive influence on the phase distribution and microstructure evolution in FeSeTe superconductors.
In the Fe(Te, Se) system, rapid cooling or high growth rates promote elemental segregation of Te and Se at the microscale, resulting in phase separation into Te-rich and Se-rich nanodomains. The work of Masi et al. confirms that rapid cooling promotes Te/Se elemental segregation in melt-processed FeSe0.5Te0.5, giving rise to a phase-separated microstructure consisting of a Te-rich tetragonal matrix and Se-rich dendrites [8]. This compositional and structural heterogeneity directly degrades the superconducting performance, evidenced by a reduction in Tc. Terao et al. further demonstrated through single-crystal growth experiments that a large temperature gradient induces an inhomogeneous distribution of Se and Te, leading to the broadening of XRD peaks and a degradation in the sharpness of the superconducting transition [107]. In addition, a comparative study by Galluzzi et al. on Fe(Se, Te) samples synthesized via the Bridgman and Self-flux methods revealed that the Bridgman-grown sample, benefiting from a slower cooling rate and superior temperature control, exhibits a higher Jc and a more homogeneous microstructure [117]. The 2020 study by Masi et al. further elucidated that while rapid quenching from high temperature preserves the high-temperature hexagonal phase and leads to a coarse core-shell microstructure detrimental to superconducting performance, optimized annealing (e.g., at 440 °C for 740 h) can significantly enhance the current carrying capability: the Jc at 4.2 K increased from 0.6 × 10⁴ A/cm2 to 1 × 10⁴ A/cm2 at self-field, and from 0.1 × 10⁴ A/cm2 to 0.3 × 10⁴ A/cm2 at 5 T, accompanied by a markedly reduced field dependence [101]. Moreover, nanoscale Te/Se phase separation, manifested as hexagonal phase regions and compositional fluctuations, has been linked to rapid crystal growth in Fe(Se, Te) systems [118,119]. In conclusion, controlling the temperature gradient and cooling rate during directional solidification presents an effective strategy for tailoring elemental distribution and grain orientation, thereby mitigating macro-segregation and optimizing superconducting performance.
Thermal processing, including annealing and cyclic sintering, is a critical post-processing step for optimizing the phase purity, microstructure. Investigations confirm that the annealing temperature is a decisive parameter for controlling the phase composition and elemental distribution within the material. For instance, annealing at 550 °C effectively mitigates compositional inhomogeneity within the primary tetragonal phase and enhances superconducting uniformity [100]. In contrast, prolonged annealing at 680 °C facilitates the transformation of dendritic precipitates from a core-shell to a lamellar morphology. This structural evolution promotes elemental interdiffusion, induces the separation of distinct superconducting phases, and significantly improves both the high-field Jc and flux pinning capability [102]. The evolution of secondary phases is also governed by the annealing temperature. For example, a high-temperature hexagonal phase can transform into either a trigonal Fe7Se8-type or an orthorhombic FeTe2-type structure [101]. Multiple sintering cycles have been shown to effectively reduce the content of non-superconducting secondary phases and enhance the superconducting volume fraction. As reported by Miao et al., three-cycle sintering yields the best performance, achieving a self-field Jc of 1.77 × 10⁴ A/cm2 at 4 K [120]. Simultaneously, heat treatment is utilized to control the size and distribution of magnetic secondary phases, such as Fe7(Te, Se)8, alleviate structural stress, and facilitate elemental homogenization [118,121]. These processes collectively inhibit harmful phase separation, which in turn results in a synergistic improvement of the superconducting and magnetic performance. In summary, a rationally designed heat treatment process facilitates the formation of the primary FeSeTe phase and reduces the content of non-superconducting phases, resulting in a systematic improvement of the overall superconducting properties [100,101,102].
Three doping strategies are compared: Co, F, and Cl. Co (<1 at%) substitutes Fe sites. The highest Jc is maintained from 0 to 5 T. Co is thus preferred for high-field applications. F transforms disordered phase separation into an ordered lamellar structure. The Δκ pinning mechanism is introduced. This strategy works best in the mid-field range (2–4 T). Cl improves Jc, but only slightly. Therefore, Co doping is recommended for high-field use. Unlike REBCO and Bi-2212, where phase separation produces insulating secondary phases, FeSeTe exhibits elemental segregation (Se-rich vs. Te-rich domains). This difference arises from the miscibility gap in the Fe-Se-Te system. The unique advantage of FeSeTe is that phase separation can be transformed from a disordered flower-like pattern into a macroscopically ordered lamellar structure through F doping. This ordered structure introduces a distinct Δκ pinning mechanism, which is not observed in cuprate superconductors. Furthermore, trace Co doping (<1 at%) achieves the highest Jc across the entire 0–5 T range by substituting Fe sites and slightly contracting the lattice. These mechanisms make FeSeTe a unique system for studying composition-driven pinning engineering. Compared with the complex oxides and iron-based systems discussed above, MgB2 features a simpler crystal structure and a different pinning landscape, as detailed in Section 4.
4. The Role of Boron and Magnesium Powders in Defining MgB2 Microstructure
The quality of the boron precursor is a primary determining factor. High-purity (e.g., 99%) amorphous boron powders with a nanoscale particle size are fundamental for achieving superior superconducting properties [122]. Nanosized boron facilitates the formation of fine MgB2 grains. This is crucial because grain boundaries are the dominant flux pinning centers; a higher density of grain boundaries directly enhances Jc, particularly in high magnetic fields [11,123,124]. The crystallinity of boron further dictates its reactivity [11]. Amorphous boron is more reactive than crystalline boron. This higher reactivity promotes MgB2 formation at lower temperatures and facilitates finer grain sizes [122]. Crystalline boron, by contrast, is less reactive and tends to produce larger grains, reducing grain boundary density and leading to lower Jc. These differences have important implications for MgB2 processing. Conversely, the use of lower-purity boron powders (e.g., 90% or 96%) introduces oxide impurities like B2O3 and results in larger, less reactive particles, significantly degrading performance even after purification attempts.
The magnesium precursor is equally important; precise control of the Mg:B molar ratio, ideally 1:2, is required to avoid the formation of non-superconducting secondary phases such as MgB4 or residual Mg. The reactivity of magnesium necessitates stringent control over oxygen exposure. MgO is an almost ubiquitous secondary phase in MgB2 samples. While a fine dispersion of nanoscale MgO particles can contribute to flux pinning [11,125], excessive formation of this phase is detrimental. Bulk MgO segregates at grain boundaries, severely disrupting intergranular connectivity, broadening the superconducting transition, and reducing the effective cross-sectional area for supercurrent flow. Therefore, handling of Mg powder in an inert atmosphere (e.g., an argon-filled glovebox) is imperative to minimize oxidation [126].
Mechanical milling of precursor powders is a widely adopted strategy to enhance performance. High-energy ball milling refines particle size, increases surface area, and introduces crystallographic defects and internal strain. These defects can evolve into effective pinning centers in the final sintered material. The milling parameters must be optimized carefully. Insufficient milling yields limited benefits, whereas excessive milling can introduce contaminants from the milling media (e.g., Fe, W, C) and cause particle agglomeration, ultimately degrading performance. The use of a process control agent, such as toluene during wet milling, is often employed to prevent excessive cold welding and oxidation, resulting in finer and cleaner powders. An alternative and highly effective method for particle refinement is ultrasonication. This technique can fracture inexpensive microcrystalline boron into nanoscale particles without the contamination risks associated with ball milling, leading to enhanced grain boundary pinning in the final MgB2 bulk.
MgB2 exhibits significant potential for medium-field applications due to its relatively high-Tc (~39 K), low raw material cost, and absence of weak-link problems [127,128,129,130]. Its superconducting properties are strongly influenced by grain size and secondary phase distribution [120,131]. This introduction will establish the focus of this chapter, optimizing the superconducting properties of MgB2 by controlling phase separation through tailored composition and processing.
4.1. Doping and Nano-Additives: Engineering Flux Pinning at the Powder Stage
MgB2 superconductors are typically synthesized via solid-state reaction, either from Mg and B powders (in situ route) or from pre-reacted MgB2 powder (ex situ route). The characteristics of the boron powder, including whether it is amorphous or crystalline, its purity, and its particle size, are considered to play a decisive role in determining the reaction kinetics, phase formation, and ultimately the superconducting properties [131]. Likewise, dopants such as SiC, C, or Y2O3 are introduced through powder mixing or ball milling, and the dispersion homogeneity of these nano-additives is known to directly influence the density and distribution of flux pinning centers [16,17]. The introduction of specific dopants or second-phase nanoparticles represents one of the most effective strategies for tailoring the microstructure of MgB2 and inducing beneficial phase separation.
Research indicates that even at low doping levels (x > 0.04), macroscopic phase separation occurs in carbon-doped MgB2. Papagelis et al. confirmed via AC magnetic susceptibility measurements that the MgB2−xCx (0 ≤ x ≤ 0.1) system exhibits multi-phase coexistence at x > 0.04, while still maintaining full diamagnetism [132]. This phenomenon was initially demonstrated by Maurin et al. using high-resolution synchrotron X-ray diffraction, which revealed extremely low carbon solid solubility and the presence of multiple AlB2-type structural phases with distinct lattice parameters a when x > 0.04, although a single-step superconducting transition was still observed in DC magnetization. Subsequent studies have shown that controlled nanoscale carbon doping can effectively introduce flux pinning centers, substantially enhancing Jc [124]. Through Raman spectroscopy, Arvanitidis et al. found that at x > 0.04, the disorder-related ω peak intensity increases significantly, and the full width at half maximum of the E2g mode reflects the competing effects of weakened electron-phonon coupling and enhanced disorder [133]. Regarding Jc improvement, Yeoh et al. demonstrated that combining nano-carbon doping with high-temperature sintering (900–1000 °C) can enhance the magnetic Jc of MgB2 bulks by two orders of magnitude at 5 K and 8 T, and by 33 times at 20 K and 5 T, while transport Ic in wires increases by 5.7 times at 4.2 K and 12 T, primarily due to carbon substitution at boron sites and the homogeneous dispersion of nanoparticles [124]. In addition, Hassan et al. reported that 5% Cu doping significantly improves the response slope, detection limit, and stability of MgB2-based electrochemical sensors, extending its application to non-superconducting fields [134]. Furthermore, Ning and Shi et al. respectively demonstrated that Ag or Sn doping promotes the formation of Mg-Ag or Mg-Sn eutectic liquid phases at relatively low temperatures (around 470 °C), accelerating MgB2 phase formation and facilitating low-temperature densification and performance optimization [135,136]. Finally, Adriano et al. compared Mn and C doping effects via angle-resolved photoemission spectroscopy, revealing that both cause Fermi surface contraction of the σ band, but Mn leads to more pronounced Tc suppression due to magnetic impurity-induced Abrikosov-Gorkov spin-flip scattering that disrupts Cooper pairs [137].
Compared to SiC-added samples with equivalent nominal content, the (Si + C) samples exhibit greater contraction along the a-axis and a higher carbon substitution level (x), leading to more significant Tc suppression and lattice distortion [138]. Although carbon substitution enhances the potential for high-field performance, magnetic measurements reveal that at an addition level of 5 wt.%, SiC doping yields a higher Jc at both 5 K and 20 K. This is attributed to the formation of effective flux pinning centers such as Mg2Si generated by the reaction of SiC, while avoiding excessive Mg loss and the formation of secondary phases caused by intense reactions in the (Si + C) sample. Consequently, SiC is considered a superior dopant for low-field applications around 20 K. Dou et al. achieved synergistic substitution of Si and C at B sites through SiC nanoparticle doping [17], introducing high density dislocations and nanoscale impurities within grains as effective pinning centers, which significantly enhanced current carrying performance. Under optimal doping, the sample reached a Jc of 1.8 × 10⁴ A/cm2 at 20 K and 4 T, with a Tc suppression of only 2.6 K. Sumption et al. [139] doped wires with 10 mol% SiC and applied a 900 °C heat treatment, effectively increasing the upper critical field and intra-grain pinning strength. This resulted in an Hirr of 18 T at 4.2 K and a maximum pinning force density (Fp) as high as 20 GN/m3, primarily due to enhanced electron scattering and the formation of effective pinning centers introduced by SiC. Yamamoto et al. [140] pointed out that whether B4C or SiC is used as the carbon source, their influence on the superconducting properties of MgB2 generally depends on the carbon substitution level for boron, specifically manifested as a-axis contraction, Tc decrease, and high-field Jc improvement. However, SiC enables effective carbon doping even under low-temperature synthesis conditions, whereas B4C relies more on high-temperature reactions, giving SiC a processing advantage. Hapipi et al. [16] demonstrated that co-adding 5 wt.% SiC and MgH2 in ex situ MgB2 can suppress high-temperature decomposition of MgB2, thereby improving the purity of the main superconducting phase and enhancing intergranular connectivity. Their study revealed that the co-doped sample exhibits a significantly refined and densified microstructure compared to samples doped with SiC alone. This microstructural optimization, characterized by finer grain size and improved connectivity, provides continuous pathways for supercurrent flow and is a key factor contributing to the high self-field Jc of 2.25 × 10⁴ A/cm2 achieved at 20 K [16].
Further analysis indicates that the enhanced performance also originates from the in situ formation of numerous nanoscale features within the co-doped sample, such as whisker-like MgO nanostructures and Mg2Si secondary phases [16]. These nanoscale precipitates act as effective flux pinning centers, substantially enhancing the current-carrying capability under applied magnetic fields. Therefore, the co-doping of SiC and MgH2 enables the synergistic optimization of both intergranular connectivity, which governs macroscopic current percolation, and nanoscale pinning centers, which govern microscopic flux pinning, leading to an overall improvement in the superconducting properties of MgB2.
The efficacy of various doping schemes in enhancing the self-field current carrying capacity of polycrystalline MgB2 is quantitatively compared in Table 5. As summarized in Table 5, the baseline Jc of undoped MgB2 polycrystals typically falls within the order of 105 A/cm2. Doping with C [124] or SiC [17,138] generally leads to a moderate improvement, elevating Jc to the range of 2.7 × 10⁵ to 7.6 × 10⁵ A/cm2. A particularly striking enhancement is observed with Ti [141] substitution in the Mg1−xTixB2 system, where a Jc of 13 × 105 A/cm2 is achieved for x = 0.1. Similarly, the addition of Y2O3 [142] nanoparticles also yields a significant boost in Jc. This compilation underscores that tailored chemical additions, which modify phase separation during processing, are a direct and effective route to engineering a higher density of flux-pinning defects and thereby improving the superconducting performance. A comparison of the field-dependent Jc behavior (Figure 13) reveals distinct trends beyond the self-field values listed in Table 5. The Ti-doped sample exhibits the highest zero-field Jc, but its performance degrades most sharply with increasing magnetic field. In contrast, the other doped systems (e.g., C, SiC, and Y2O3) show remarkably similar and more gradual Jc decay profiles over the 0–5 T range. This indicates that, while Ti doping creates exceptionally effective pinning centers at low fields, the microstructures engineered by other additives provide more stable flux-pinning landscapes under applied magnetic fields. Based on this comparison, the following recommendations are made. For mid-field applications, such as MRI magnets, SiC doping is preferred. This balances cost and high-field performance. For low-field applications, Ti doping is suitable. This maximizes the zero-field current.
Table 5.
Self-field Jc at 20 K for MgB2 polycrystals with various chemical additions.
Figure 13.
Magnetic field dependence of Jc at 20 K for MgB2 polycrystals with various chemical additions. The data for blue, black, red, green, and purple curves are from Refs. [17], [124], [138], [141], and [142], respectively.
In summary, compositional design strategies, such as the introduction of SiC nanoparticles or the co-doping of SiC with MgH2, can effectively generate a high density of nanoscale flux-pinning centers in MgB2. These strategies, when coupled with the concurrent improvement in intergranular connectivity, enable the synergistic optimization of its superconducting properties. Beyond the specific doping strategies discussed above, a broader range of approaches has been explored to optimize the MgB2 microstructure. In particular, the incorporation of metallic additives and the application of low-temperature activated sintering processes have been shown to play a crucial role in facilitating the formation of the superconducting phase, refining grain structure, and mitigating oxidation and porosity [12,16,17,142]. These effects are fundamental to achieving high-performance bulk materials.
The sintering temperature, even under high external pressure, remains a decisive factor in determining the phase composition and structural quality of MgB2. Figure 14 illustrates this dependency through XRD patterns of bulk MgB2 samples processed at temperatures ranging from 700 to 1100 °C under approximately 5 GPa pressure [143]. As the temperature increases, the MgB2 peaks sharpen and shift slightly, indicating improved crystallinity and lattice relaxation. However, beyond 900 °C, distinct diffraction peaks of MgB4 and MgO emerge, signaling the onset of significant decomposition of the superconducting phase. This temperature-induced phase separation underscores the delicate balance required in processing: excessive temperature stabilizes non-superconducting phases, degrading the overall current-carrying capability.
Figure 14.
XRD patterns of MgB2 bulk samples sintered at different temperatures under high pressure (~5 GPa). The inset highlights the evolution of the (002) and (110) peaks. Adapted from [143] under the terms of the CC BY 4.0 license.
4.2. Sintering Routes: From Powder Compacts to Dense Superconducting Bulks
The synthesis and post-processing parameters critically determine the phase purity, grain size, and distribution of secondary phases in MgB2.
Among these, low-temperature sintering technology is regarded as a highly promising approach due to its ability to effectively suppress MgO formation and reduce grain size, thereby offering the potential to enhance Jc. Huang et al. developed an innovative low-temperature sintering route utilizing Mg(BH4)2 as a precursor [144]. Their work successfully demonstrated the synthesis of MgB2 superconductors at temperatures as low as 400–500 °C. The microstructural evolution was found to be critically dependent on both sintering temperature and duration. At the initial stage (e.g., 400 °C for 2 h), the microstructure consisted of fine, isolated grains with poor intergranular connectivity. As the temperature increased and sintering time was prolonged, the grains gradually coarsened and coalesced. Ultimately, after sintering at 500 °C for 54 h, a dense microstructure with blurred grain boundaries and excellent intergranular connectivity was achieved [144].
In the fabrication of MgB2, the influence of different processing routes on phase separation and superconducting properties has been extensively investigated. Noudem et al. produced bulk MgB2 via spark plasma sintering (SPS), which exhibits levitation forces comparable to YBCO at low temperatures, demonstrating its potential for magnetic levitation applications [125]. Hapipi et al. reported that co-addition of 5 wt.% SiC and 6 mol% MgH2 at a high sintering temperature of 1000 °C significantly enhanced Jc of ex situ MgB2, reaching 22,517 A/cm2 at 20 K and self-field, while increasing the MgB2 phase fraction to 43.0% [16]. Innovative processing routes that combine shaping and densification steps are emerging to overcome the limitations of conventional sintering. One promising approach is the integration of Laser Powder Bed Fusion (L-PBF) with SPS [145]. As shown in Figure 15, this method begins with the L-PBF fabrication of a porous MgB2 preform with defined geometry. Subsequent SPS treatment using a sacrificial SiC matrix densifies the preform while preserving its macroscopic shape. The resulting microstructure exhibits a characteristic lamellar morphology with well-connected grains, which is crucial for establishing continuous superconducting current paths. This hybrid process demonstrates the feasibility of manufacturing complex-shaped MgB2 components without severely compromising the superconducting transition, which remains near 38 K. This demonstrates that additive manufacturing combined with field-assisted sintering can overcome the shape limitations of conventional MgB2 processing while retaining superconducting performance.
Figure 15.
Micrographs of an MgB2 sample processed by L-PBF + SPS: (a) starting powder, (b) sintered preform, (c) surface after SPS, (d) sintered microstructure. Adapted from [145] under the terms of the CC BY 4.0 license.
Through prolonged self-sintering at 900 °C for 96 h, Shimada et al. examined the microstructure connectivity of ex situ bulk MgB2, revealing that, despite improved packing factor, platelet-like pores and MgO agglomeration restrict current flow, with the optimal sample achieving only 21% connectivity [146]. Birajdar et al. compared various powder-in-tube (PIT) processed MgB2 wires and tapes, showing that mechanically alloyed samples exhibit superior high-field Jc due to high density and fine grains, while SiC addition in in situ tapes helps retain and form Mg2Si, improving flux pinning [147]. Appropriate post-annealing is crucial for optimizing PIT-fabricated MgB2 tapes. Matsumoto et al. demonstrated that short—time annealing at 600 °C for stainless steel-sheathed MgB2 tapes effectively heals microcracks induced by cold rolling and enhances intergranular electrical connectivity, leading to an order-of-magnitude increase in Jc under high fields (e.g., 10 T) [122]. Furthermore, Sklyarova et al. combined laser powder bed fusion (L-PBF) with SPS to fabricate complex-shaped MgB2 components with a superconducting transition temperature of 38 K, highlighting the potential of additive manufacturing for superconducting applications [145].
Based on the above findings, the superconducting properties of MgB2 are closely linked to phase separation phenomena occurring during processing. The superior high-field Jc observed in optimally processed MgB2 can be directly correlated with the nanoscale defect structure introduced during sintering. Figure 16 presents a direct comparison using transmission electron microscopy [143]. In a sample sintered at 900 °C under high pressure, a dense network of dislocations is clearly visible within the MgB2 grains. These lattice defects act as effective flux-pinning centers, enhancing the material’s ability to retain superconductivity in applied magnetic fields. In contrast, the microstructure of a sample processed at 1100 °C shows significantly coarsened grains with few remaining dislocations, as most defects have been annealed out. This loss of intragranular pinning sites explains the rapid degradation of Jc at high fields for samples sintered at excessively high temperatures, highlighting the critical importance of preserving beneficial crystal defects during processing.
Figure 16.
TEM images of MgB2 grains sintered at (a) 900 °C and (b) 1100 °C under high pressure. Dense dislocations in (a) provide strong flux pinning, while defects are annealed out in (b). Adapted from [143] under the terms of the CC BY 4.0 license.
Through composition design, such as the introduction of nano-additives like SiC, a high density of nanoscale secondary phases can be in situ generated to serve as effective flux pinning centers. Meanwhile, precise control of sintering parameters helps suppress the formation of detrimental phases (e.g., coarse MgO) and promotes fine, uniformly distributed phase separation, along with optimized grain boundary structure. Future research may focus on the synergistic effects of multiple dopants, the development of novel nano-additives, and more refined process control tailored to practical conductor forms such as wires and tapes, aiming to further enhance the performance of MgB2 across broader temperature and magnetic field ranges.
In summary, Table 6 [16,126,144,146,148] compiles Jc values of MgB2 bulk superconductors fabricated under different processing conditions. The compiled data demonstrate that tailoring sintering parameters and incorporating selected nano-additives can markedly improve the current carrying capacity. These findings underscore the decisive role of processing pathway design in refining the microstructure. This enhances both intergranular current percolation and flux pinning effectiveness. The performance of MgB2 is critically determined by the microstructure shaped during processing. Figure 17 compares the magnetic field dependence of Jc at 20 K for samples fabricated via the distinct routes listed in Table 6. Specimens prepared through optimized conventional sintering or precursor based low-temperature routes demonstrate more gradual Jc decay, indicative of a more robust and field-stable pinning architecture. This highlights that the choice of processing pathway governs not only the density of pinning centers but also their effectiveness under applied magnetic fields.
Table 6.
Comparison of Jc values for MgB2 bulk superconductors processed under different conditions. Data are extracted from literature [16,126,144,146,148] for measurements at 20 K and applied fields of 0 T or 0.2 T.
Figure 17.
Magnetic field dependence of Jc at 20 K for MgB2 polycrystals fabricated via the processing routes summarized in Table 6. The data for black, purple, red, blue, and green curves are from Refs. [16], [126], [144], [146], and [148], respectively.
A key distinction of MgB2 from REBCO and Bi-2212 is the absence of weak-link behavior at grain boundaries. Consequently, grain refinement directly enhances Jc by increasing grain boundary density, rather than introducing secondary phase pinning centers. This explains why nanosized amorphous boron powder is critical for achieving high performance in MgB2. Another unique feature is the role of MgO. While coarse MgO particles are detrimental, a fine dispersion of nanoscale MgO can contribute to flux pinning. This dual role is not seen in cuprate systems. Furthermore, compared with FeSeTe, MgB2 offers a simpler processing window (e.g., low-temperature sintering at 500 °C using Mg(BH4)2 precursor), making it suitable for mid-field applications such as MRI magnets. However, its relatively low Tc (39 K) limits its use to cryogenic temperatures.
5. Cross-System Comparative Synthesis
Despite their different material chemistries, a common principle is identified across the four systems: REBCO, Bi-2212, FeSeTe, and MgB2. The characteristics of precursor powders include particle size, phase purity, morphology, and doping homogeneity. These characteristics control the scale and uniformity of phase-separated microstructures. They in turn determine superconducting performance. Finer and more homogeneous powders lead to finer RE-211 particles in REBCO, more uniform phase distribution in Bi-2212, better controlled Se/Te segregation in FeSeTe, and higher grain boundary density in MgB2. Thus, powder engineering is a universal strategy across all four systems.
However, the specific manifestations of phase separation differ fundamentally. For REBCO, insulating RE-211 secondary phases are formed via peritectic reactions. For Bi-2212, the detrimental Bi-2201 phase is induced by excessive doping (e.g., Na > 0.02 at%) during sintering, which causes the Bi-2212 phase to break down. FeSeTe exhibits a different behavior. Elemental segregation occurs due to a miscibility gap, producing Se-rich and Te-rich domains. This is unique among the four systems. Turning to MgB2, grain boundaries serve as the dominant pinning centers, with MgO precipitation as a secondary feature. The absence of weak-link behavior at MgB2 grain boundaries distinguishes it from the cuprate systems. These differences mean that a unified mechanistic analogy does not exist. Nevertheless, the common dependence on powder characteristics remains.
Doping strategies across the four systems can be classified into three functional types: microstructural refinement, introduction of new pinning interfaces, and direct creation of additional pinning centers. The Δκ pinning strategy in FeSeTe has no direct counterpart in REBCO or Bi-2212. Whether ordered phase separation can be achieved in other systems therefore remains an open question.
6. Conclusions and Outlook
In this review, the critical role of solidification-induced phase separation in governing the microstructure and superconducting properties of four major practical superconductors, namely REBCO, Bi-2212, FeSeTe, and MgB2, has been systematically examined. Across these distinct material systems, a consistent principle can be identified: the path from powder precursors to final performance is fundamentally shaped by phase separation phenomena. The characteristics of the starting powders, including particle size, purity, morphology, and doping homogeneity, are considered to set the initial conditions for all subsequent microstructural evolution.
The discussion emphasizes two primary and interrelated microstructural control strategies, compositional design and process engineering. For REBCO superconductors, the refinement of RE-211 precipitates is achieved through the addition of elements or compounds such as CeO2, Pt, and BaO2. Superior microstructural homogeneity over the TSMG process is provided by the TSIG technique, which avoids peritectic decomposition. In the case of Bi-2212, enhanced phase stability and material densification are obtained by doping with Ag, Na, or Pb, followed by optimized melting and ultra-high-pressure heat treatments. Regarding FeSeTe materials, disordered phase separation can be transformed into an ordered layered structure via strategic doping with elements like F or Co. This structural ordering introduces effective Δκ flux-pinning centers, while subsequent controlled cooling and annealing processes are crucial for achieving homogeneity. Within the MgB2 system, improved grain connectivity and a high density of nanoscale flux-pinning defects are simultaneously introduced. This is accomplished by the incorporation of nanoparticles such as SiC alongside advanced sintering techniques, including SPS or FAST processing routes.
Among the four systems, REBCO has the most extensive literature on powder-processing relationships, Bi-2212 features a unique overpressure processing technique, FeSeTe exhibits a distinctive Δκ pinning mechanism, and MgB2 benefits from low raw material cost and weak-link-free grain boundaries. Future work should focus on several technically specific areas: optimizing doping uniformity in REBCO, clarifying the mechanism of overpressure processing in Bi-2212, establishing quantitative pinning models in FeSeTe, scaling up low-temperature routes for MgB2 wires, and exploring multi-component doping across all four systems.
Author Contributions
Z.Z. was responsible for literature search, data collection, analysis, and drafting of the manuscript. M.T. conceptualized the research framework and critically revised the manuscript for intellectual content and structure. H.Z. and W.R. participated in preliminary literature sorting. S.Y. and D.W. provided academic guidance. Y.M. provided resource support, supervised the research, and approved the final version. All authors have read and agreed to the published version of the manuscript.
Funding
This work is partially supported by the National Natural Science Foundation of China (Grant Nos. 52588101, 52377032, 52377033), the CAS Superconducting Research Project under Grant No. SCZX-0103, the Science and Technology Research Foundation of Institute of Electrical Engineering of Chinese Academy of Sciences under Grant No. IEERF250204, Beijing Municipal Science & Technology Commission, Administrative Commission of Zhongguancun Science Park No. Z251100003625029, the International Partnership Program of Chinese Academy of Sciences (Grant No. 116GJHZ2023005MI).
Data Availability Statement
No new data were created or analyzed in this study.
Acknowledgments
I appreciate the support from the Institute of Electrical Engineering, Chinese Academy of Sciences and the University of Jinan during the course of this work.
Conflicts of Interest
The authors declare that they have no known competing financial interests or personal relationships that could have appeared to influence the work reported in this paper.
References
- Namburi, D.K.; Shi, Y.H.; Cardwell, D.A. The processing and properties of bulk (RE)BCO high temperature superconductors: Current status and future perspectives. Supercond. Sci. Technol. 2021, 34, 053002. [Google Scholar] [CrossRef] [Scilit]
- Jetybayeva, A.; Mukanova, A.; Nurpeissova, A.; Bakenov, Z.; Petrykin, V.; Lee, S. REBCO superconductors by pulsed laser deposition: Key innovations and large-scale applications. Iscience 2025, 28, 113260. [Google Scholar] [CrossRef] [Scilit]
- Shiohara, Y.; Endo, A. Crystal growth of bulk high-Tc superconducting oxide materials. Mater. Sci. Eng. R Rep. 1997, 19, 1–86. [Google Scholar] [CrossRef] [Scilit]
- MacManus-Driscoll, J.L.; Wimbush, S.C. Processing and application of high-temperature superconducting coated conductors. Nat. Rev. Mater. 2021, 6, 587–604. [Google Scholar] [CrossRef] [Scilit]
- Larbalestier, D.C.; Jiang, J.; Trociewitz, U.P.; Kametani, F.; Scheuerlein, C.; Dalban-Canassy, M.; Matras, M.; Chen, P.; Craig, N.C.; Lee, P.J.; et al. Isotropic round-wire multifilament cuprate superconductor for generation of magnetic fields above 30 T. Nat. Mater. 2014, 13, 375–381. [Google Scholar] [CrossRef] [Scilit]
- Bruzzone, P.; Fietz, W.H.; Minervini, J.V.; Novikov, M.; Yanagi, N.; Zhai, Y.H.; Zheng, J.X. High temperature superconductors for fusion magnets. Nucl. Fusion 2018, 58, 103001. [Google Scholar] [CrossRef] [Scilit]
- Scanlan, R.M.; Malozemoff, A.P.; Larbalestier, D.C. Superconducting materials for large scale applications. Proc. IEEE 2004, 92, 1639–1654. [Google Scholar] [CrossRef] [Scilit]
- Masi, A.; Alvani, C.; Augieri, A.; Bellusci, M.; Celentano, G.; Marzi, G.D.; Fabbri, F.; Zignani, C.F.; Barbera, A.L.; Padella, F.; et al. Phase separation and microstructure in superconducting FeSe1−xTex materials. IEEE Trans. Appl. Supercond. 2018, 28, 7300305. [Google Scholar] [CrossRef]
- Liu, J.X.; Zhang, S.N.; Li, M.; Sang, L.N.; Li, Z.; Cheng, Z.X.; Zhao, W.Y.; Feng, J.Q.; Li, C.S.; Zhang, P.X.; et al. Boosting superconducting properties of Fe(Se, Te) via dual-oscillation phenomena induced by fluorine doping. ACS Appl. Mater. Interfaces 2019, 11, 18825–18832. [Google Scholar] [CrossRef] [Scilit]
- Sun, Q.; Xu, Z.T.; Dong, C.H.; Huang, H.; Wang, D.L.; Zhang, X.P.; Ma, Y.W. Macroscopically ordered phase separation: A new strategy for improving the superconducting performance in Fe(Se, Te). Mater. Today Adv. 2023, 17, 100354. [Google Scholar] [CrossRef] [Scilit]
- Muralidhar, M.; Shadab, M.; Srikanth, A.S.; Jirsa, M.; Jacques, N. Review on high-performance bulk MgB2 superconductors. J. Phys. D Appl. Phys. 2024, 57, 053001. [Google Scholar] [CrossRef] [Scilit]
- Ma, Z.Q.; Liu, Y.C. Low-temperature synthesis of MgB2 superconductors. Int. Mater. Rev. 2011, 56, 267–286. [Google Scholar] [CrossRef] [Scilit]
- Babu, N.H.; Shi, Y.H.; Pathak, S.K.; Dennis, A.R.; Cardwell, D.A. Developments in the processing of bulk (RE)BCO superconductors. Phys. C 2011, 471, 169–178. [Google Scholar] [CrossRef] [Scilit]
- Namburi, D.K.; Shi, Y.H.; Palmer, K.G.; Dennis, A.R.; Durrell, J.H.; Cardwell, D.A. Control of Y-211 content in bulk YBCO superconductors fabricated by a buffer-aided, top seeded infiltration and growth melt process. Supercond. Sci. Technol. 2016, 29, 034007. [Google Scholar] [CrossRef] [Scilit]
- Liu, J.; Zhang, S.; Sang, L.; Li, M.; Zhao, W.; Li, Z.; Cheng, Z.; Liu, L.; Feng, J.; Li, C.; et al. Enhancement of superconducting properties in polycrystalline Fe(Se, Te) via a dual coordination effect. Scr. Mater. 2019, 169, 19–22. [Google Scholar] [CrossRef] [Scilit]
- Mohd Hapipi, N.; Chen, S.K.; Shaari, A.H.; Awang Kechik, M.M.; Lim, K.P.; Kamarudin, A.N.; Shabdin, M.K.; Tan, K.B.; Lee, O.J.; Miryala, M. Enhancing critical current density in ex-situ MgB2 via high-temperature sintering with SiC and MgH2 additives. Phys. B 2025, 718, 417882. [Google Scholar] [CrossRef] [Scilit]
- Dou, S.X.; Pan, A.V.; Zhou, S.; Ionescu, M.; Liu, H.K.; Munroe, P.R. Substitution-induced pinning in MgB2 superconductor doped with SiC nano-particles. Supercond. Sci. Technol. 2002, 15, 1587. [Google Scholar] [CrossRef] [Scilit]
- Alade, I.O.; Rahaman, M.S.; Qahtan, T.F. A comprehensive review of superconductivity research productivity. J. Supercond. Nov. Magn. 2022, 35, 2621–2637. [Google Scholar] [CrossRef] [Scilit]
- Maeda, H.; Yanagisawa, Y. Recent developments in high-temperature superconducting magnet technology (Review). IEEE Trans. Appl. Supercond. 2014, 24, 4602412. [Google Scholar] [CrossRef] [Scilit]
- Bussmann-Holder, A.; Keller, H. High-temperature superconductors: Underlying physics and applications. Z. Fur Naturfor Schung Sect. B J. Chem. Sci. 2020, 75, 3–14. [Google Scholar] [CrossRef] [Scilit]
- Bednorz, J.G.; Müller, K.A. Possible high Tc superconductivity in the Ba−La−Cu−O system. Z. Phys. B Condens. Matter. 1986, 64, 189–193. [Google Scholar] [CrossRef] [Scilit]
- Antončík, F.; Sedmidubský, D.; Jiříčková, A.; Lojka, M.; Hlásek, T.; Růžička, K.; Jankovský, O. Thermodynamic properties of stoichiometric non-superconducting phase Y2BaCuO5. Materials 2019, 12, 3163. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Nariki, S.; Sakai, N.; Murakami, M.; Hirabayashi, I. High critical current density in RE–Ba–Cu–O bulk superconductors with very fine RE2BaCuO5 particles. Phys. C 2004, 412-414, 557–565. [Google Scholar] [CrossRef] [Scilit]
- Namburi, D.K.; Shi, Y.H.; Palmer, K.G.; Dennis, A.R.; Durrell, J.H.; Cardwell, D.A. An improved top seeded infiltration growth method for the fabrication of Y-Ba-Cu-O bulk superconductors. J. Eur. Ceram. Soc. 2016, 36, 615–624. [Google Scholar] [CrossRef] [Scilit]
- Ouerghi, A.; Moutalbi, N.; Noudem, J.G.; M’Chirgui, A. The influence of slow cooling on Y211 size and content in single-grain YBCO bulk superconductor through the infiltration-growth process. Phys. C 2017, 534, 37–44. [Google Scholar] [CrossRef] [Scilit]
- Cardwell, D.A.; Shi, Y.H.; Numburi, D.K. Reliable single grain growth of (RE)BCO bulk superconductors with enhanced superconducting properties. Supercond. Sci. Technol. 2020, 33, 024004. [Google Scholar] [CrossRef] [Scilit]
- Thoma, M.; Shi, Y.; Dennis, T.; Durrell, J.; Cardwell, D. Effect of Y-211 particle size on the growth of single grain Y–Ba–Cu–O bulk superconductors. J. Cryst. Growth 2015, 412, 31–39. [Google Scholar] [CrossRef] [Scilit]
- Kim, S.-J.; Kim, H.-G. Effects of 211 inclusions on zone melt-textured (RE/Y)–Ba–Cu–O superconductors. Phys. C 2000, 338, 110–114. [Google Scholar] [CrossRef] [Scilit]
- Xu, C.; Hu, A.; Sakai, N.; Izumi, M.; Hirabayashi, I. Effect of BaO2 and fine Gd2BaCuO7−δ addition on the superconducting properties of air-processed GdBa2Cu3O7−δ. Supercond. Sci. Technol. 2005, 18, 229. [Google Scholar] [CrossRef] [Scilit]
- Shi, Y.; Hari Babu, N.; Iida, K.; Cardwell, D.A. Properties of GdBCO bulk superconductors melt-processed in air using a Mg-doped Nd–Ba–Cu–O generic seed crystal. Supercond. Sci. Technol. 2007, 20, 38. [Google Scholar] [CrossRef] [Scilit]
- Zhai, W.; Shi, Y.; Durrell, J.H.; Dennis, A.R.; Zhang, Z.; Cardwell, D.A. Processing and properties of bulk Y-Ba-Cu-O superconductors fabricated by top seeded melt growth from precursor pellets containing a graded CeO2 composition. Cryst. Growth Des. 2015, 15, 907–914. [Google Scholar] [CrossRef] [Scilit]
- Zhao, W.; Shi, Y.; Radušovská, M.; Dennis, A.R.; Durrell, J.H.; Diko, P.; Cardwell, D.A. Comparison of the effects of platinum and CeO2 on the properties of single grain, Sm–Ba–Cu–O bulk superconductors. Supercond. Sci. Technol. 2016, 29, 125002. [Google Scholar] [CrossRef] [Scilit]
- Shlyk, L.; Nenkov, K.; Krabbes, G.; Fuchs, G. Melt-processed YBCO with Pt or Ce additions: Comparison of pinning behavior. Phys. C 2005, 423, 22–28. [Google Scholar] [CrossRef] [Scilit]
- Cui, Y.; Yang, W. Enhanced performance of GdBCO bulk superconductors by doping a new kind of YGdBa4CuNbOy nanoparticles. Supercond. Sci. Technol. 2024, 37, 035002. [Google Scholar] [CrossRef] [Scilit]
- Shi, Y.; Babu, N.H.; Iida, K.; Cardwell, D.A. The effect of very high barium content in the precursor on the properties of GdBCO single grain bulk superconductors. J. Mater. Res. 2009, 24, 10–18. [Google Scholar] [CrossRef] [Scilit]
- Li, Z.; Ida, T.; Miki, M.; Izumi, M. Trapped flux behavior in melt-growth GdBCO bulk superconductor under off-axis field cooled magnetization. IEEE Trans. Appl. Supercond. 2017, 27, 6800604. [Google Scholar] [CrossRef] [Scilit]
- Lo, W.; Cardwell, D.A.; Dewhurst, C.D.; Leung, H.T.; Chow, J.C.L.; Shi, Y.H. Controlled processing and properties of large Pt-doped Y–Ba–Cu–O pseudocrystals for electromagnetic applications. J. Mater. Res. 1997, 12, 2889–2900. [Google Scholar] [CrossRef] [Scilit]
- Shi, Y.; Hari Babu, N.; Iida, K.; Yeoh, W.K.; Dennis, A.R.; Cardwell, D.A. The influence of Gd-2411(Nb) on the superconducting properties of GdBCO/Ag single grains. Supercond. Sci. Technol. 2009, 22, 075025. [Google Scholar] [CrossRef] [Scilit]
- Hari Babu, N.; Iida, K.; Cardwell, D.A. Flux pinning in melt-processed nanocomposite single-grain superconductors. Supercond. Sci. Technol. 2007, 20, S141. [Google Scholar] [CrossRef] [Scilit]
- Muralidhar, M.; Koblischka, M.R.; Diko, P.; Murakami, M. Enhancement of Jc by 211 particles in ternary (Nd0.33Eu0.33Gd0.33)Ba2Cu3Oy melt-processed superconductors. Appl. Phys. Lett. 2000, 76, 91–93. [Google Scholar] [CrossRef] [Scilit]
- Zhai, W.; Shi, Y.; Durrell, J.H.; Dennis, A.R.; Cardwell, D.A. The influence of Y-211 content on the growth rate and Y-211 distribution in Y-Ba-Cu-O single grains fabricated by top seeded melt growth. Cryst. Growth Des. 2014, 14, 6367–6375. [Google Scholar] [CrossRef] [Scilit]
- Endo, A.; Chauhan, H.S.; Egi, T.; Shiohara, Y. Macrosegregation of Y2Ba1Cu1O5 particles in Y1Ba2Cu3O7−δ crystals grown by an undercooling method. J. Mater. Res. 1996, 11, 795–803. [Google Scholar] [CrossRef] [Scilit]
- Hlásek, T.; Shi, Y.; Durrell, J.H.; Dennis, A.R.; Namburi, D.K.; Plecháček, V.; Rubešová, K.; Cardwell, D.A.; Jankovský, O. Cost-effective isothermal top-seeded melt-growth of single-domain YBCO superconducting ceramics. Solid State Sci. 2019, 88, 74–80. [Google Scholar] [CrossRef] [Scilit]
- Abulaiti, A.; Yang, W.M.; Wu, T.T.; Cui, Y.L. The effect of pre-sintering and high-temperature infiltration on the properties of single-domain YBCO bulk superconductors by the Y+011 top-seeded infiltration growth process. Supercond. Sci. Technol. 2023, 36, 025005. [Google Scholar] [CrossRef] [Scilit]
- Kuchárová, V.; Diko, P.; Volochová, D.; Antal, V.; Lojka, M.; Hlásek, T.; Plecháček, V. Microstructure and superconducting properties of bulk EuBCO-Ag with and without holes. J. Eur. Ceram. Soc. 2022, 42, 6533–6541. [Google Scholar] [CrossRef] [Scilit]
- Reddy, E.S.; Rajasekharan, T. Fabrication of textured REBa2Cu3O7/RE2BaCuO5 (RE = Y, Gd) composites by infiltration and growth of RE2BaCuO5 preforms by liquid phases. Supercond. Sci. Technol. 1998, 11, 523. [Google Scholar] [CrossRef] [Scilit]
- Namburi, D.K.; Shi, Y.; Palmer, K.G.; Dennis, A.R.; Durrell, J.H.; Cardwell, D.A. A novel, two-step top seeded infiltration and growth process for the fabrication of single grain, bulk (RE)BCO superconductors. Supercond. Sci. Technol. 2016, 29, 095010. [Google Scholar] [CrossRef] [Scilit]
- Matsumoto, K.; Mele, P. Artificial pinning center technology to enhance vortex pinning in YBCO coated conductors. Supercond. Sci. Technol. 2010, 23, 014001. [Google Scholar] [CrossRef] [Scilit]
- Goyal, A.; Kang, S.; Leonard, K.J.; Martin, P.M.; Gapud, A.A.; Varela, M.; Paranthaman, M.; Ijaduola, A.O.; Specht, E.D.; Thompson, J.R.; et al. Irradiation-free, columnar defects comprised of self-assembled nanodots and nanorods resulting in strongly enhanced flux-pinning in YBa2Cu3O7−δ films. Supercond. Sci. Technol. 2005, 18, 1533. [Google Scholar] [CrossRef] [Scilit]
- Yang, W.M.; Zhou, L.; Feng, Y.; Zhang, P.X.; Zhang, C.P. The effect of temperature gradient on the morphology of YBCO bulk superconductors by melt texture growth processing. J. Alloys Compd. 2006, 415, 276–279. [Google Scholar] [CrossRef] [Scilit]
- Diko, P.; Pagáčová, R.; Zmorayová, K.; Kuchárová, V.; Vojtková, L.; Antal, V.; Kavečanský, V. Influence of addition of nanosize barium cerate on the microstructure and properties of top-seeded melt growth YBCO bulk superconductors. J. Am. Ceram. Soc. 2021, 104, 740–752. [Google Scholar] [CrossRef] [Scilit]
- Kim, C.-J.; Park, H.-W.; Kim, K.-B.; Lee, K.-W.; Gye-Won Hong, G.-W.H. Preparation and critical current density of melt-textured Y-Ba-Cu-O superconductor containing fine Y2BaCuO5 inclusions. Jpn. J. Appl. Phys. 1995, 34, L671. [Google Scholar] [CrossRef] [Scilit]
- Wang, M.; Yang, W.-M.; Li, J.-W.; Feng, Z.-L.; Yang, P.-T. Comparison of the superconducting properties in GdBCO bulk superconductors fabricated with two different solid phases. Supercond. Sci. Technol. 2015, 28, 035004. [Google Scholar] [CrossRef] [Scilit]
- Wang, M.; Yang, P.-t.; Yang, W.-m.; Li, J.-w.; Hassan, Q.U.I. The fabrication process of a high performance and pure c-axis grown GdBCO bulk superconductor with the TSMT-IG technique. Supercond. Sci. Technol. 2015, 28, 105011. [Google Scholar] [CrossRef] [Scilit]
- Namburi, D.K.; Shi, Y.; Dennis, A.R.; Durrell, J.H.; Cardwell, D.A. A robust seeding technique for the growth of single grain (RE)BCO and (RE)BCO–Ag bulk superconductors. Supercond. Sci. Technol. 2018, 31, 044003. [Google Scholar] [CrossRef] [Scilit]
- Pavel, D. Growth-related microstructure of melt-grown REBa2Cu3Oy bulk superconductors. Supercond. Sci. Technol. 2000, 13, 1202. [Google Scholar] [CrossRef] [Scilit]
- Shen, T.M.; Li, P.; Ye, L.Y. Heat treatment control of Bi-2212 coils: I. Unravelling the complex dependence of the critical current density of Bi-2212 wires on heat treatment. Cryogenics 2018, 89, 95–101. [Google Scholar] [CrossRef] [Scilit]
- Jiang, J.Y.; Bradford, G.; Hossain, S.I.; Brown, M.D.; Cooper, J.; Miller, E.; Huang, Y.B.; Miao, H.P.; Parrell, J.A.; White, M.; et al. High-performance Bi-2212 round wires made with recent powders. IEEE Trans. Appl. Supercond. 2019, 29, 6400405. [Google Scholar] [CrossRef] [Scilit]
- Sager, D.; Meier, L.P.; Gauckler, L.J.; Chen, M. Influence of precursor calcination parameters on the critical current density of Bi-2212 superconductors. Phys. C 2006, 434, 125–134. [Google Scholar] [CrossRef] [Scilit]
- Zhang, Y.; Koch, C.C.; Schwartz, J. Formation of Bi2Sr2CaCu2Ox/Ag multifilamentary metallic precursor powder-in-tube wires. Supercond. Sci. Technol. 2016, 29, 125005. [Google Scholar] [CrossRef] [Scilit]
- Nane, O.; Özçelik, B.; Amaveda, H.; Sotelo, A.; Madre, M.A. Improvement of structural and superconducting properties of Bi-2212 textured rods by substituting sodium. Ceramurg. Int. 2016, 42, 8473–8477. [Google Scholar] [CrossRef] [Scilit]
- Nane, O.; Özçelik, B.; Sotelo, A.; Madre, M.A. Effect of Na substitution on superconducting properties of Bi-2212 ceramics prepared by sinter-forged process. J. Eur. Ceram. Soc. 2017, 37, 1007–1012. [Google Scholar] [CrossRef] [Scilit]
- Zhang, S.N.; Ma, X.B.; Cui, L.J.; Huang, Y.J.; Li, C.S.; Feng, J.Q.; Yan, G.; Zhang, P.X. Influences of Na doping on superconducting properties of Bi-2212 high temperature superconductors. Rare Met. Mater. Eng. 2020, 49, 1184–1190. [Google Scholar]
- Shin, D.C.; Kang, S.-J.L.; Chung, H.-S. Dendrite formation in the Bi2Sr2CaCu2O8–Ag system: Reactions between Ag and oxide melt. Phys. C 2000, 340, 141–148. [Google Scholar] [CrossRef] [Scilit]
- Hamid, N.A.; Abd-Shukor, R. Effects of TiO2 addition on the superconducting properties of Bi-Sr-Ca-Cu-O system. J. Mater. Sci. 2000, 35, 2325–2329. [Google Scholar] [CrossRef] [Scilit]
- Margulies, L.; Dennis, K.W.; Kramer, M.J.; McCallum, R.W. Effect of P(O2) and Ag content on the decompisition pathway of Bi2Sr2CaCu2Ox. Phys. C 1996, 266, 62–74. [Google Scholar] [CrossRef] [Scilit]
- Wong-Ng, W.K.; Cook, L.P.; Jiang, F. Melting equilibria of the Bi-Sr-Ca-Cu-O (BSCCO) system in air: The primary crystallization phase field of the 2212 phase and the effect of silver addition. J. Am. Ceram. Soc. 1998, 81, 1829–1838. [Google Scholar] [CrossRef] [Scilit]
- Hiroi, Z.; Chong, I.; Takano, M. Two-phase microstructures generating efficient pinning centers in the heavily Pb-substituted Bi2Sr2CaCu2O8+δ single crystals. J. Solid State Chem. 1998, 138, 98–110. [Google Scholar] [CrossRef] [Scilit]
- Togano, K.; Kumakura, H.; Maeda, H.; Yanagisawa, E.; Takahashi, K. Properties of Pb-doped Bi-Sr-Ca-Cu-O superconductors. Appl. Phys. Lett. 1988, 53, 1329–1331. [Google Scholar] [CrossRef] [Scilit]
- Atilla, C.; Ahmet, E.; Bekir, Ö. Superconductivity of Bi1.6Pb0.4Sr2Ca3Cu4O12. Chin. Phys. Lett. 2002, 19, 1863. [Google Scholar] [CrossRef] [Scilit]
- Kumar, J.; Ahluwalia, P.K.; Kishan, H.; Awana, V.P.S. Significant improvement in superconductivity by substituting Pb at Bi-site in Bi2-xPbxSr2CaCu2O8 with x=0.0 to 0.40. J. Supercond. Nov. Magn. 2010, 23, 493–499. [Google Scholar] [CrossRef] [Scilit]
- Liu, H.; Liu, L.; Zhang, Y.; Yu, H.; Jin, Z. Melting of the 2212 phase in Bi(Pb)SrCaCuO system. J. Mater. Sci. 1999, 34, 6095–6098. [Google Scholar] [CrossRef] [Scilit]
- Holesinger, T.G.; Kennison, J.A.; Marken, K.R.; Hanping, M.; Meinesz, M.; Campbell, S. Compositional and microstructural analysis of high Ic and Jc Bi-2212 conductors. IEEE Trans. Appl. Supercond. 2005, 15, 2562–2565. [Google Scholar] [CrossRef]
- Cabassi, R.; Delmonte, D.; Abbas, M.M.; Abdulridha, A.R.; Gilioli, E. The role of chemical substitutions on Bi-2212 superconductors. Crystals 2020, 10, 462. [Google Scholar] [CrossRef] [Scilit]
- Zhang, S.; Li, C.; Hao, Q.; Lu, T.; Zhang, P. Influences of Yb substitution on the intergrain connections and flux pinning properties of Bi-2212 superconductors. Phys. C 2015, 511, 26–32. [Google Scholar] [CrossRef] [Scilit]
- Zhang, S.; Li, C.; Hao, Q.; Ma, X.; Lu, T.; Zhang, P. Optimization of Bi-2212 high temperature superconductors by potassium substitution. Supercond. Sci. Technol. 2015, 28, 045014. [Google Scholar] [CrossRef] [Scilit]
- Xu, A.X.; Jiang, J.Y.; Tarantini, C.; Kametani, F.; Hellstrom, E.; Larbalestier, D.C. Flux Pinning Enhancement of Bi-2212 Tapes by Increasing Sr Content. IEEE Trans. Appl. Supercond. 2024, 34, 6400505. [Google Scholar] [CrossRef] [Scilit]
- Nachtrab, W.T.; Renaud, C.V.; Wong, T.; Liu, X.T.; Shen, T.M.; Trociewitz, U.P.; Schwartz, J. Development of high superconductor fraction Bi2Sr2CaCu2Ox/Ag wire for MRI. IEEE Trans. Appl. Supercond. 2008, 18, 1184–1187. [Google Scholar] [CrossRef]
- Tarantini, C.; Barua, S.; Oloye, T.A.; Kametani, F.; Jiang, J.Y.; Hellstrom, E.E.; Larbalestier, D.C. Variation of effective filament diameter, irreversibility field, anisotropy, and pinning efficiency in Bi-2212 round wires. Supercond. Sci. Technol. 2024, 37, 015021. [Google Scholar] [CrossRef] [Scilit]
- Jiang, J.Y.; Hossain, S.I.; Barua, S.; Oloye, T.A.; Kvitkovic, J.; Kametani, F.; Trociewitz, U.P.; Hellstrom, E.E.; Larbalestier, D.C.; Bugaris, D.E.; et al. Performance and Microstructure Variation with Maximum Heat Treatment Temperature for Recent Bi-2212 Round Wires. IEEE Trans. Appl. Supercond. 2023, 33, 6400105. [Google Scholar] [CrossRef] [Scilit]
- Cheggour, N.; Marks, E.L.; Jiang, J.Y.; Bosque, E.; Larbalestier, D.C. Densification Effects on Critical-Current Dependence on Longitudinal Strain in Bi2Sr2CaCu2O8+x Wires. IEEE Trans. Appl. Supercond. 2025, 35, 8400911. [Google Scholar] [CrossRef] [Scilit]
- Oz, Y.; Davis, D.; Jiang, J.; Hellstrom, E.E.; Larbalestier, D.C. Influence of twist pitch on hysteretic losses and transport Jc in overpressure processed high Jc Bi-2212 round wires. Supercond. Sci. Technol. 2022, 35, 064004. [Google Scholar] [CrossRef] [Scilit]
- Jiang, J.Y.; Kvitkovic, J.; Linville, C.; Brown, J.; Jones, J.; Davis, D.S.; Kim, Y.; Kametani, F.; Trociewitz, U.P.; Hellstrom, E.E.; et al. Effects of Rolling Reduction on Critical Current Density and Microstructure of Bi-2212 Wires. IEEE Trans. Appl. Supercond. 2025, 35, 6400105. [Google Scholar] [CrossRef] [Scilit]
- Holesinger, T.G.; Miller, D.J.; Chumbley, L.S. Melt processing of the Bi2Sr2CaCu2Oy superconductor in oxygen and argon atmospheres. IEEE Trans. Appl. Supercond. 1993, 3, 1178–1181. [Google Scholar] [CrossRef]
- Marinkovic, B.A.; Xia, S.K.; Serra, E.T.; Rizzo, F. Influence of processing parameters of partial-melting process on phase assemblage, microstructure and superconducting properties of Bi-2212 bulk material. Mater. Chem. Phys. 2005, 91, 301–312. [Google Scholar] [CrossRef] [Scilit]
- Kameneva, M.Y.; Kozeeva, L.P.; Podberezskaya, N.V.; Naumov, D.Y.; Kurat’eva, N.V.; Fedorov, V.E. Composite microstructures in the Bi-Sr-Ca-Cu-O system. Inorg. Mater. 2007, 43, 845–852. [Google Scholar] [CrossRef] [Scilit]
- Imayev, M.F.; Daminov, R.R.; Popov, V.A.; Kaibyshev, O.A. Melting of Bi2Sr2CaCu2O8+x ceramics under uniform compression. Inorg. Mater. 2005, 41, 537–541. [Google Scholar] [CrossRef] [Scilit]
- Hallstedt, B.; Gauckler, L.J. Revision of the thermodynamic descriptions of the Cu–O, Ag–O, Ag–Cu–O, Bi–Sr–O, Bi–Ca–O, Bi–Cu–O, Sr–Cu–O, Ca–Cu–O and Sr–Ca–Cu–O systems. Calphad 2003, 27, 177–191. [Google Scholar] [CrossRef] [Scilit]
- Kamihara, Y.; Watanabe, T.; Hirano, M.; Hosono, H. Iron-based layered superconductor La[O1−xFx]FeAs (x = 0.05–0.12) with Tc = 26 K. J. Am. Chem. Soc. 2008, 130, 3296–3297. [Google Scholar] [CrossRef] [Scilit]
- Si, Q.; Yu, R.; Abrahams, E. High-temperature superconductivity in iron pnictides and chalcogenides. Nat. Rev. Mater. 2016, 1, 16017. [Google Scholar] [CrossRef] [Scilit]
- Guo, Z.; Muraoka, K.; Gao, H.; Shimada, Y.; Harada, T.; Tokuta, S.; Hasegawa, Y.; Yamamoto, A.; Hata, S. Planar defects and strain distributions in polycrystalline BaFe2As2 superconductors synthesized by mechanochemical methods. Acta Mater. 2024, 266, 119648. [Google Scholar] [CrossRef] [Scilit]
- Iida, K. Status of iron based superconductors: Characteristics and relevant properties for applications. IEEE Trans. Appl. Supercond. 2025, 35, 7400109. [Google Scholar] [CrossRef] [Scilit]
- Liu, G.; Li, J.; Chen, K. Reaction mechanism in fast combustion synthesis of superconducting FeSe and FeSe0.7Te0.3. Acta Mater. 2017, 122, 187–198. [Google Scholar] [CrossRef] [Scilit]
- Zhao, J.; Liao, J.; Dong, C.; Wang, D.; Ma, Y. Properties and applications of iron-chalcogenide superconductors. Materials 2024, 17, 3059. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Sylva, G.; Bellingeri, E.; Bernini, C.; Celentano, G.; Ferdeghini, C.; Leveratto, A.; Lisitskiy, M.; Malagoli, A.; Manca, N.; Mancini, A.; et al. The role of texturing and thickness of oxide buffer layers in the superconducting properties of Fe(Se,Te) coated conductors. Supercond. Sci. Technol. 2020, 33, 114002. [Google Scholar] [CrossRef] [Scilit]
- Song, J.N.; Xu, Z.T.; Xiong, X.M.; Yuan, W.; Dong, C.H.; Sun, Q.; Tang, M.H.; Chen, W.P.; Tian, H.F.; Li, J.Q.; et al. Critical role played by interface engineering in weakening thickness dependence of superconducting and structural properties of FeSe0.5Te0.5-coated conductors. ACS Appl. Mater. Interfaces 2023, 15, 26215–26224. [Google Scholar] [CrossRef] [Scilit]
- Fan, F.; Xu, Z.; Cheng, Z.; Huang, H.; Zhu, Y.; Liu, S.; Dong, C.; Zhang, X.; Ma, Y. Enhanced superconducting properties of FeSe0.8Te0.2 thin films grown by pulsed laser deposition. Phys. C 2019, 564, 55–58. [Google Scholar] [CrossRef] [Scilit]
- Yuan, P.; Xu, Z.; Ma, Y.; Sun, Y.; Tamegai, T. Optimization of deposition conditions to grow high-quality Fe-Se-Te thin films. IEEE Trans. Appl. Supercond. 2017, 27, 7500105. [Google Scholar] [CrossRef] [Scilit]
- Bhatia, V.; Rodriguez, E.E.; Butch, N.P.; Paglione, J.; Green, M.A. Phase separation and superconductivity in Fe1+xTe0.5Se0.5. Chem. Commun. 2011, 47, 11297–11299. [Google Scholar] [CrossRef] [Scilit]
- Sala, A.; Palenzona, A.; Bernini, C.; Caglieris, F.; Cimberle, M.R.; Ferdeghini, C.; Lamura, G.; Martinelli, A.; Pani, M.; Putti, M. The role of Fe deficiency in FeySe0.5Te0.5 samples prepared by a melting process. Phys. C 2013, 494, 69–73. [Google Scholar] [CrossRef] [Scilit]
- Masi, A.; Alvani, C.; Armenio, A.A.; Augieri, A.; Barba, L.; Campi, G.; Celentano, G.; Chita, G.; Fabbri, F.; Zignani, C.F.; et al. Fe(Se, Te) from melting routes: The influence of thermal processing on microstructure and superconducting properties. Supercond. Sci. Technol. 2020, 33, 084007. [Google Scholar] [CrossRef] [Scilit]
- Masi, A.; Alvani, C.; Augieri, A.; Bellusci, M.; Celentano, G.; Marzi, G.D.; Fabbri, F.; Zignani, C.F.; Barbera, A.L.; Padella, F.; et al. Fe(Se, Te) from melting routes: Insight on phase separation. IEEE Trans. Appl. Supercond. 2019, 29, 7300304. [Google Scholar] [CrossRef]
- Yeh, K.-W.; Huang, T.-W.; Huang, Y.-l.; Chen, T.-K.; Hsu, F.-C.; Wu, P.M.; Lee, Y.-C.; Chu, Y.-Y.; Chen, C.-L.; Luo, J.-Y.; et al. Tellurium substitution effect on superconductivity of the α-phase iron selenide. EPL 2008, 84, 37002. [Google Scholar] [CrossRef] [Scilit]
- Palenzona, A.; Sala, A.; Bernini, C.; Braccini, V.; Cimberle, M.R.; Ferdeghini, C.; Lamura, G.; Martinelli, A.; Pallecchi, I.; Romano, G.; et al. A new approach for improving global critical current density in Fe(Se0.5Te0.5) polycrystalline materials. Supercond. Sci. Technol. 2012, 25, 115018. [Google Scholar] [CrossRef] [Scilit]
- Chen, N.; Liu, Y.; Ma, Z.; Li, H. Significant enhancement of superconducting properties in the FeSe0.5Te0.5 bulks by minor Sn addition. Mater. Lett. 2016, 175, 16–19. [Google Scholar] [CrossRef] [Scilit]
- McQueen, T.M.; Huang, Q.; Ksenofontov, V.; Felser, C.; Xu, Q.; Zandbergen, H.; Hor, Y.S.; Allred, J.; Williams, A.J.; Qu, D.; et al. Extreme sensitivity of superconductivity to stoichiometry in Fe1+δSe. Phys. Rev. B 2009, 79, 014522. [Google Scholar] [CrossRef] [Scilit]
- Terao, K.; Kashiwagi, T.; Shizu, T.; Klemm, R.A.; Kadowaki, K. Superconducting and tetragonal-to-orthorhombic transitions in single crystals of FeSe1−xTex (0 ≤ x ≤ 0.61). Phys. Rev. B 2019, 100, 224516. [Google Scholar] [CrossRef] [Scilit]
- Sales, B.C.; Sefat, A.S.; McGuire, M.A.; Jin, R.Y.; Mandrus, D.; Mozharivskyj, Y. Bulk superconductivity at 14 K in single crystals of Fe1+yTexSe1−x. Phys. Rev. B 2009, 79, 094521. [Google Scholar] [CrossRef] [Scilit]
- Zhang, A.M.; Xia, T.L.; Kong, L.R.; Xiao, J.H.; Zhang, Q.M. Effects on superconductivity of transition-metal doping in FeSe0.5Te0.5. J. Phys. Condens. Matter. 2010, 22, 245701. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Gawryluk, D.J.; Fink-Finowicki, J.; Wiśniewski, A.; Puźniak, R.; Domukhovski, V.; Diduszko, R.; Kozłowski, M.; Berkowski, M. Growth conditions, structure and superconductivity of pure and metal-doped FeTe1−xSex single crystals. Supercond. Sci. Technol. 2011, 24, 065011. [Google Scholar] [CrossRef] [Scilit]
- Liu, C.Y.; Zhang, H.; Zhao, K.; Cai, F.G.; Yang, X.S.; Zhao, Y. Increased critical current density in iron selenide telluride crystals doping with trace amount of cobalt. J. Appl. Phys. 2025, 137, 073901. [Google Scholar] [CrossRef] [Scilit]
- Liu, J.; Shao, B.; Liu, X.; Li, M.; Sang, L.; Zhang, W.; Zhang, S.; Feng, J.; Li, C.; Dou, S.; et al. Improving superconducting performance of Fe(Se, Te) with in situ formed grain-boundary strengthening and flux pinning centers. ACS Appl. Mater. Interfaces 2022, 14, 2246–2254. [Google Scholar] [CrossRef] [Scilit]
- Masi, A.; Alvani, C.; Armenio, A.A.; Augieri, A.; Celentano, G.; De Marzi, G.; Fabbri, F.; Zignani, C.F.; La Barbera, A.; Padella, F.; et al. Fe(Se, Te) system crystallized in molten chlorides flux: The obtained materials and their characterization. J. Cryst. Growth 2019, 528, 125268. [Google Scholar] [CrossRef] [Scilit]
- Mizuguchi, Y.; Tomioka, F.; Tsuda, S.; Yamaguchi, T.; Takano, Y. Substitution effects on FeSe superconductor. J. Phys. Soc. Jpn. 2009, 78, 074712. [Google Scholar] [CrossRef] [Scilit]
- Tsurkan, V.; Deisenhofer, J.; Günther, A.; Kant, C.; Klemm, M.; von Nidda, H.A.K.; Schrettle, F.; Loidl, A. Physical properties of FeSe0.5Te0.5 single crystals grown under different conditions. Eur. Phys. J. B 2011, 79, 289–299. [Google Scholar] [CrossRef] [Scilit]
- Liu, J.X.; Li, C.S.; Zhang, S.N.; Feng, J.Q.; Zhang, P.X.; Zhou, L. Fabrication of Fe1.1Se0.5Te0.5 bulk by a high energy ball milling technique. Solid State Commun. 2017, 267, 39–41. [Google Scholar] [CrossRef] [Scilit]
- Galluzzi, A.; Buchkov, K.; Tomov, V.; Nazarova, E.; Kovacheva, D.; Leo, A.; Grimaldi, G.; Pace, S.; Polichetti, M. Mixed state properties of iron based Fe(Se, Te) superconductor fabricated by Bridgman and by self-flux methods. J. Appl. Phys. 2018, 123, 233904. [Google Scholar] [CrossRef] [Scilit]
- Wittlin, A.; Aleshkevych, P.; Przybylińska, H.; Gawryluk, D.J.; Dłużewski, P.; Berkowski, M.; Puźniak, R.; Gutowska, M.U.; Wiśniewski, A. Microstructural magnetic phases in superconducting FeTe0.65Se0.35. Supercond. Sci. Technol. 2012, 25, 065019. [Google Scholar] [CrossRef] [Scilit]
- Hu, H.; Zuo, J.-M.; Wen, J.; Xu, Z.; Lin, Z.; Li, Q.; Gu, G.; Park, W.K.; Greene, L.H. Phase separation in the iron chalcogenide superconductor Fe1+yTexSe1−x. New J. Phys. 2011, 13, 053031. [Google Scholar] [CrossRef] [Scilit]
- Miao, C.; Liu, L.; Li, Y. Effect of the cycle number of multistep sintering on the properties of FeSe0.4Te0.6 superconductors. J. Am. Ceram. Soc. 2024, 107, 6172–6179. [Google Scholar] [CrossRef] [Scilit]
- Xing, X.; Sun, Y.; Yi, X.; Li, M.; Feng, J.; Meng, Y.; Zhang, Y.; Li, W.; Zhou, N.; He, X.; et al. Electronic transport properties and hydrostatic pressure effect of FeSe0.67Te0.33 single crystals free of phase separation. Supercond. Sci. Technol. 2021, 34, 055006. [Google Scholar] [CrossRef] [Scilit]
- Matsumoto, A.; Hatakeyama, H.; Kitaguchi, H.; Togano, K.; Kumakura, H. The superconducting properties of MgB2/(stainless steel) tapes fabricated by the PIT process. IEEE Trans. Appl. Supercond. 2003, 13, 3225–3228. [Google Scholar] [CrossRef]
- Matsushita, T.; Kiuchi, M.; Yamamoto, A.; Shimoyama, J.; Kishio, K. Critical current density and flux pinning in superconducting MgB2. Phys. C 2008, 468, 1833–1835. [Google Scholar] [CrossRef] [Scilit]
- Yeoh, W.K.; Kim, J.H.; Horvat, J.; Xu, X.; Qin, M.J.; Dou, S.X.; Jiang, C.H.; Nakane, T.; Kumakura, H.; Munroe, P. Control of nano carbon substitution for enhancing the critical current density in MgB2. Supercond. Sci. Technol. 2006, 19, 596. [Google Scholar] [CrossRef] [Scilit]
- Noudem, J.G.; Bernstein, P.; Dupont, L.; Martin, F.G.R.; Sotelo, G.G.; Dias, D.H.N.; de Andrade, R.; Muralidhar, M.; Murakami, M. Spark plasma sintering of bulk MgB2 and levitation force measurements. Supercond. Sci. Technol. 2020, 33, 024001. [Google Scholar] [CrossRef] [Scilit]
- Muralidhar, M.; Higuchi, M.; Jirsa, M.; Diko, P.; Kokal, I.; Murakami, M. Improved critical current densities of bulk MgB2 using carbon-coated amorphous boron. IEEE Trans. Appl. Supercond. 2017, 27, 6201104. [Google Scholar] [CrossRef] [Scilit]
- Liu, M.-X.; Gan, Z.-Z. The upper critical field in two-band layered superconductors. Chin. Phys. 2007, 16, 826. [Google Scholar] [CrossRef] [Scilit]
- Gallitto, A.A.; Bonsignore, G.; Vigni, M.L.; Giunchi, G.; Nefyodov, Y.A. Microwave response of a cylindrical cavity made of bulk MgB2 superconductor. Phys. C 2008, 468, 66–71. [Google Scholar] [CrossRef] [Scilit]
- Iwasa, Y. HTS and NMR/MRI magnets: Unique features, opportunities, and challenges. Phys. C 2006, 445–448, 1088–1094. [Google Scholar] [CrossRef] [Scilit]
- Nagamatsu, J.; Nakagawa, N.; Muranaka, T.; Zenitani, Y.; Akimitsu, J. Superconductivity at 39 K in magnesium diboride. Nature 2001, 410, 63–64. [Google Scholar] [CrossRef] [Scilit]
- Matthews, G.A.B.; Santra, S.; Ma, R.; Grovenor, C.R.M.; Grant, P.S.; Speller, S.C. Effect of the sintering temperature on the microstructure and superconducting properties of MgB2 bulks manufactured by the field assisted sintering technique. Supercond. Sci. Technol. 2020, 33, 054003. [Google Scholar] [CrossRef] [Scilit]
- Papagelis, K.; Arvanitidis, J.; Margadonna, S.; Iwasa, Y.; Takenobu, T.; Pissas, M.; Prassides, K. Phase separation in carbon-doped MgB2 studied by means of alternating current susceptibility measurements. J. Phys. Condens. Matter. 2002, 14, 7363. [Google Scholar] [CrossRef] [Scilit]
- Arvanitidis, J.; Papagelis, K.; Prassides, K.; Kourouklis, G.A.; Ves, S.; Takenobu, T.; Iwasa, Y. Raman spectroscopic study of carbon substitution in MgB2. J. Phys. Chem. Solids. 2004, 65, 73–77. [Google Scholar] [CrossRef] [Scilit]
- Hassan, S.S.M.; Fathy, M.A. A novel solid-state iodide ion-selective electrode based on copper-doped MgB2 superconductor. Microchem. J. 2025, 218, 115639. [Google Scholar] [CrossRef] [Scilit]
- Ning, B.Q.; Jiang, H.; Yan, Z.S. Sintering mechanism of Ag-doped MgB2 superconductor from low temperature to high temperature. J. Mater. Sci.-Mater. Electron. 2010, 21, 666–670. [Google Scholar] [CrossRef] [Scilit]
- Shi, Q.Z.; Jiang, H.; Yan, Z.S. Phase formation sequences and mechanism of MgB2 superconductor with minor Sn doping. J. Mater. Sci.-Mater. Electron. 2010, 21, 1240–1243. [Google Scholar] [CrossRef] [Scilit]
- Adriano, C.; Xu, M.; Huyan, S.; Pakuszewski, K.R.; Machado, A.P.; Schrunk, B.; Bud′ko, S.L.; Ribeiro, R.A.; Canfield, P.C.; Kaminski, A. Tuning the electronic properties of MgB2 by substitution with Mn and C. J. Phys. Condens. Matter 2025, 37, 305502. [Google Scholar] [CrossRef] [Scilit]
- Chen, S.K.; Tan, K.Y.; Tan, K.B.; Shaari, A.H.; Kursumovic, A.; MacManus-Driscoll, J.L. Optimizing C incorporation into magnesium diboride. IEEE Trans. Appl. Supercond. 2011, 21, 2627–2630. [Google Scholar] [CrossRef] [Scilit]
- Sumption, M.D.; Bhatia, M.; Dou, S.X.; Rindfliesch, M.; Tomsic, M.; Arda, L.; Ozdemir, M.; Hascicek, Y.; Collings, E.W. Irreversibility field and flux pinning in MgB2 with and without SiC additions. Supercond. Sci. Technol. 2004, 17, 1180. [Google Scholar] [CrossRef] [Scilit]
- Yamamoto, A.; Shimoyama, J.; Ueda, S.; Katsura, Y.; Horii, S.; Kishio, K. Doping effects on critical current properties of MgB2 bulks synthesized by modified powder-in-tube method. IEEE Trans. Appl. Supercond. 2005, 15, 3292–3295. [Google Scholar] [CrossRef]
- Zhao, Y.; Feng, Y.; Cheng, C.H.; Zhou, L.; Wu, Y.; Machi, T.; Fudamoto, Y.; Koshizuka, N.; Murakami, M. High critical current density of MgB2 bulk superconductor doped with Ti and sintered at ambient pressure. Appl. Phys. Lett. 2001, 79, 1154–1156. [Google Scholar] [CrossRef] [Scilit]
- Wang, J.; Bugoslavsky, Y.; Berenov, A.; Cowey, L.; Caplin, A.D.; Cohen, L.F.; MacManus Driscoll, J.L.; Cooley, L.D.; Song, X.; Larbalestier, D.C. High critical current density and improved irreversibility field in bulk MgB2 made by a scaleable, nanoparticle addition route. Appl. Phys. Lett. 2002, 81, 2026–2028. [Google Scholar] [CrossRef] [Scilit]
- Gao, Z.; Santra, S.; Amirkhanlou, S.; Eardley, E.; Wort, C.; Grovenor, C.R.M.; Speller, S.C. Microstructures and superconducting properties of MgB2 bulk samples processed by ultra-high pressure-assisted sintering. J. Eur. Ceram. Soc. 2022, 42, 7481–7490. [Google Scholar] [CrossRef] [Scilit]
- Huang, Z.; Cai, X.; Xi, D.; Luo, W.; Guo, C.; Feng, Q.; Nie, R.; Wang, F.; Gan, Z. Low-temperature sintering to fabricate MgB2 by using Mg(BH4)2 as precursor. Supercond. Sci. Technol. 2021, 34, 075007. [Google Scholar] [CrossRef] [Scilit]
- Sklyarova, A.; Presmanes, L.; Baylac, V.; Chevallier, G.; Estournès, C.; Duployer, B.; Noudem, J.; Bernstein, P.; Tailhades, P.; Thimont, Y. Processing of bulk MgB2 superconductors by coupling laser powder bed fusion and spark plasma sintering techniques. Materials 2025, 18, 2367. [Google Scholar] [CrossRef] [Scilit]
- Shimada, Y.; Hata, S.; Ikeda, K.-i.; Nakashima, H.; Matsumura, S.; Tanaka, H.; Yamamoto, A.; Shimoyama, J.-i.; Kishio, K. Microstructural connectivity in sintered ex-situ MgB2 bulk superconductors. J. Alloys Compd. 2016, 656, 172–180. [Google Scholar] [CrossRef] [Scilit]
- Birajdar, B.; Eibl, O.; Braccini, V.; Grasso, G.; Pachla, W.; Herrman, M.; Häßler, W. Correlation of superconducting properties and microstructure of MgB2 wires and tapes. Phys. C 2007, 460–462, 1409–1410. [Google Scholar] [CrossRef] [Scilit]
- Matthews, G.A.B.; Mousavi, T.; Santra, S.; Grovenor, C.R.M.; Grant, P.S.; Speller, S. Improving the connectivity of MgB2 bulk superconductors by a novel liquid phase sintering process. Supercond. Sci. Technol. 2022, 35, 065005. [Google Scholar] [CrossRef] [Scilit]
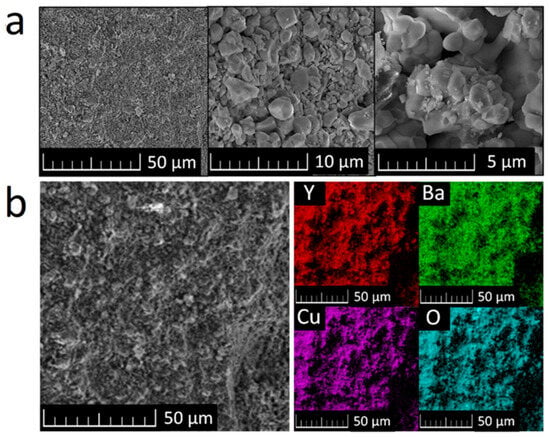
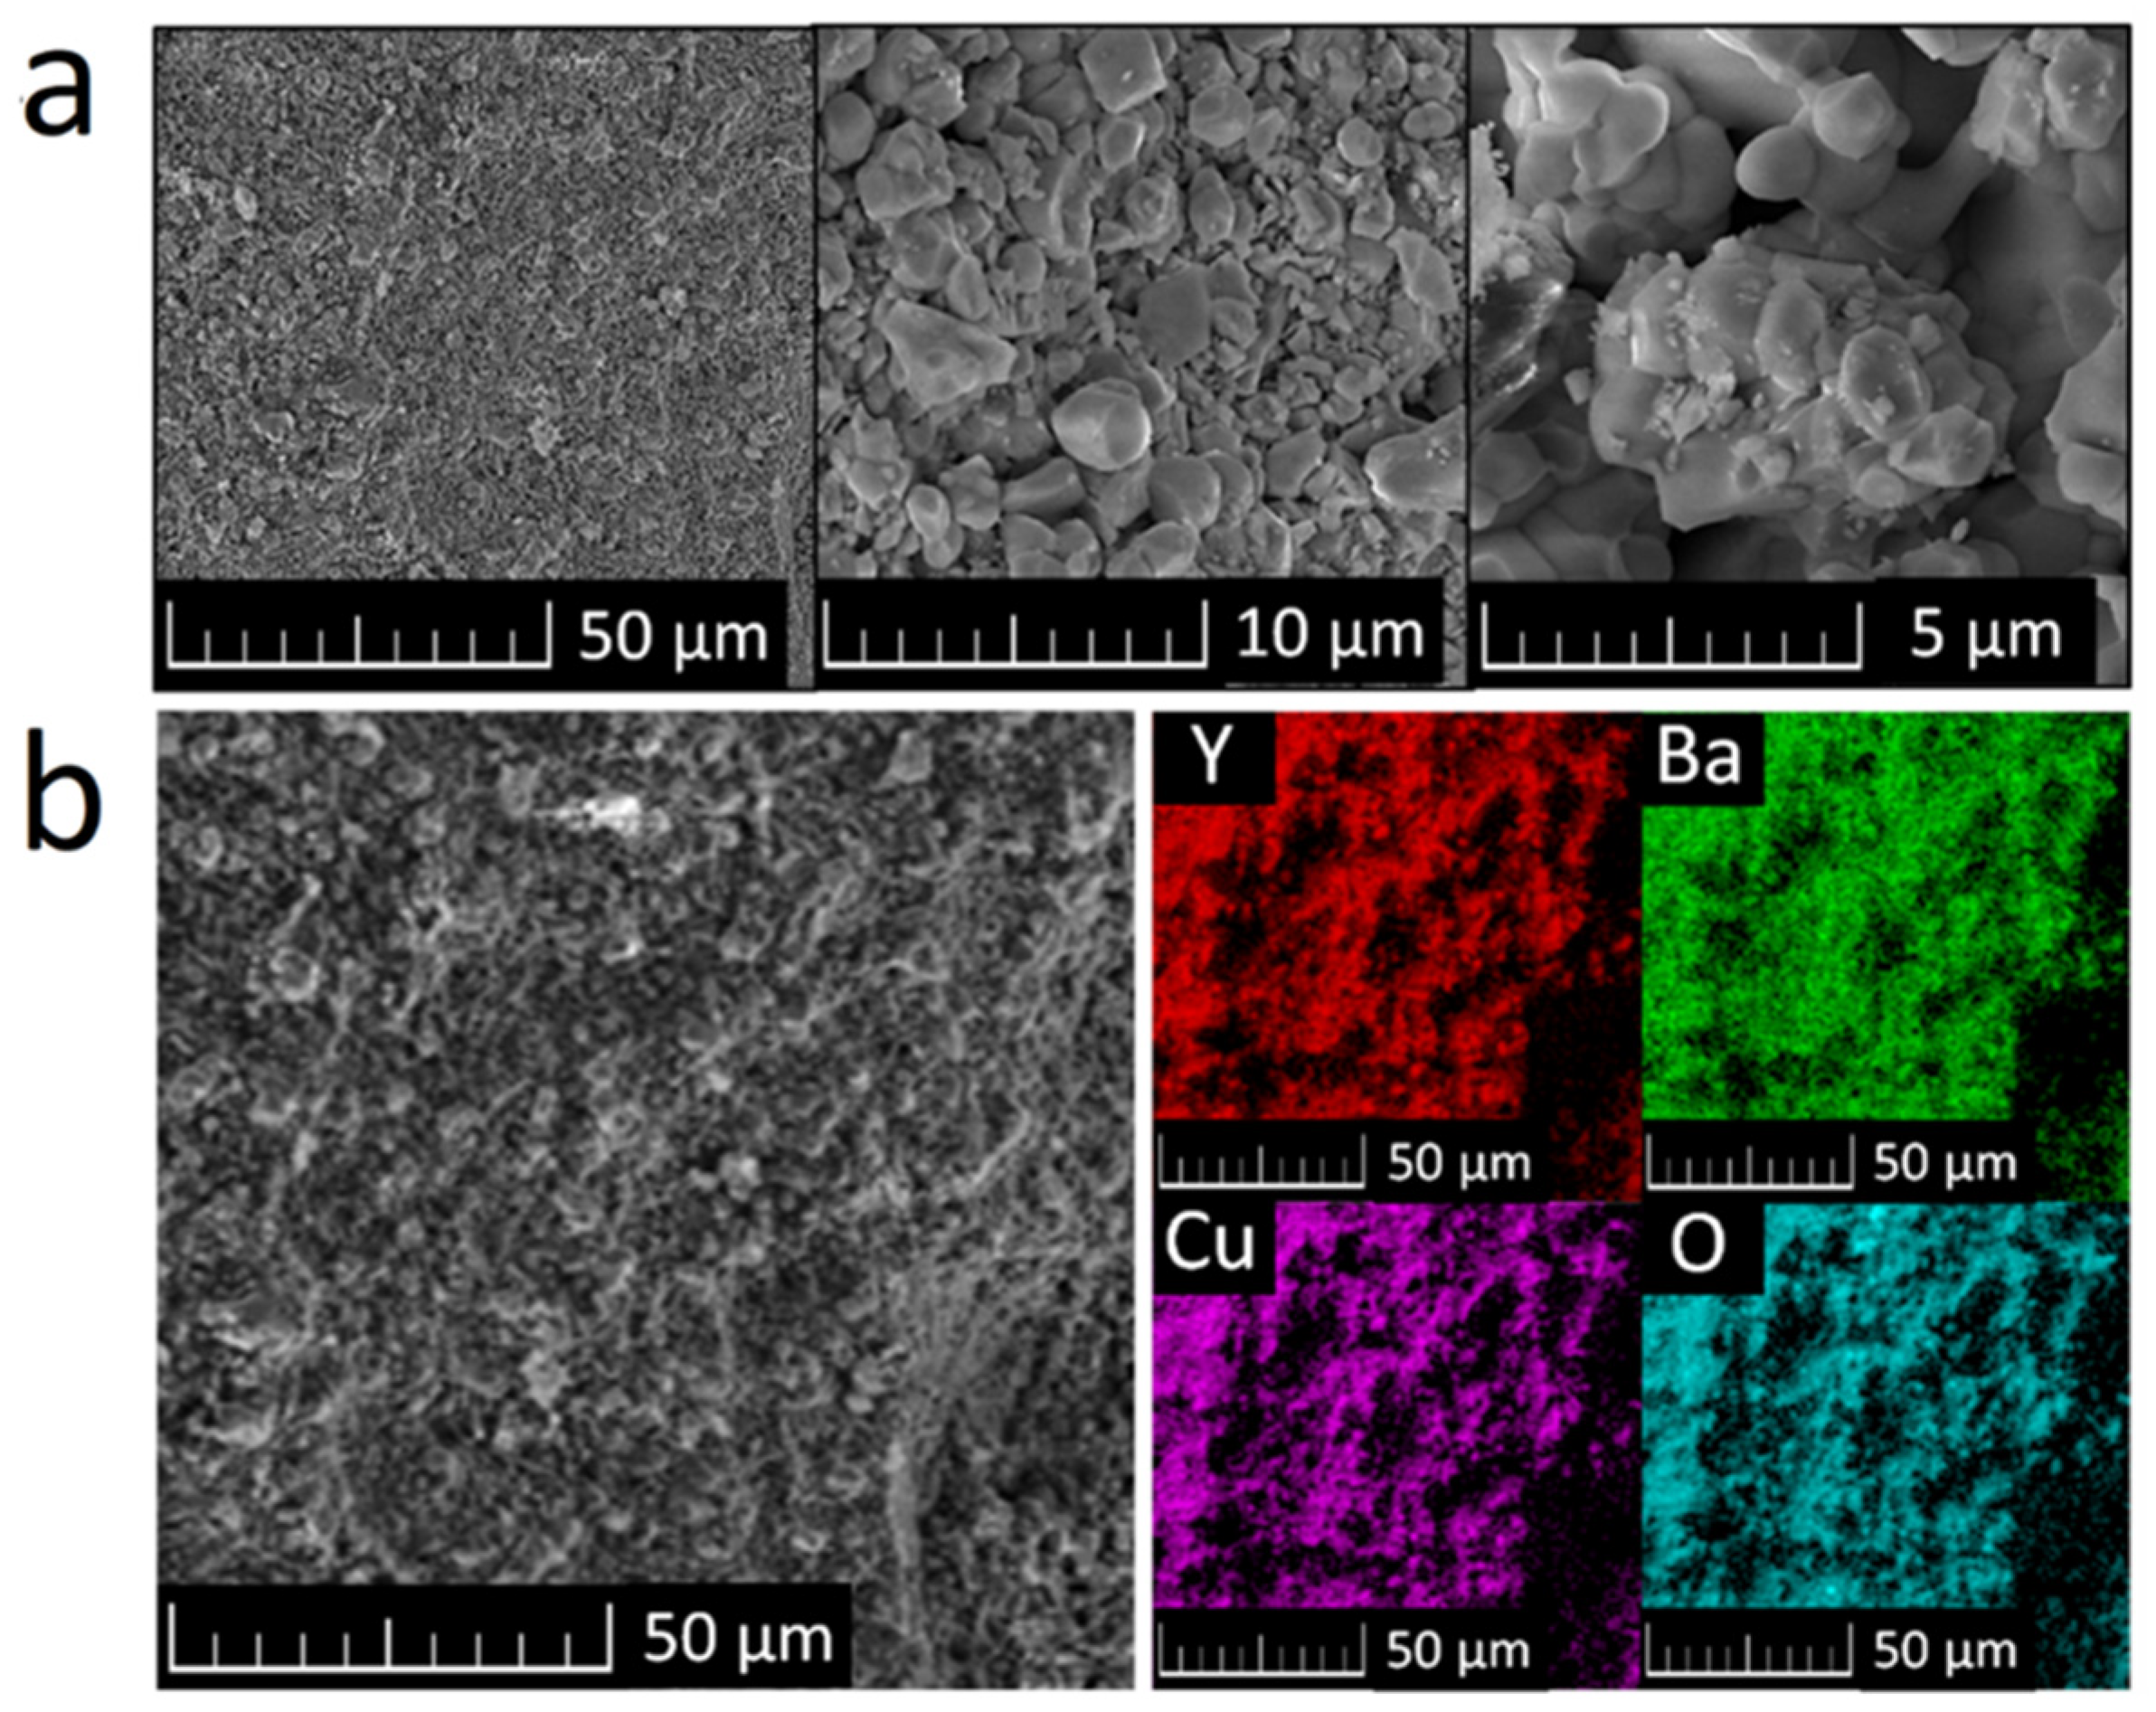
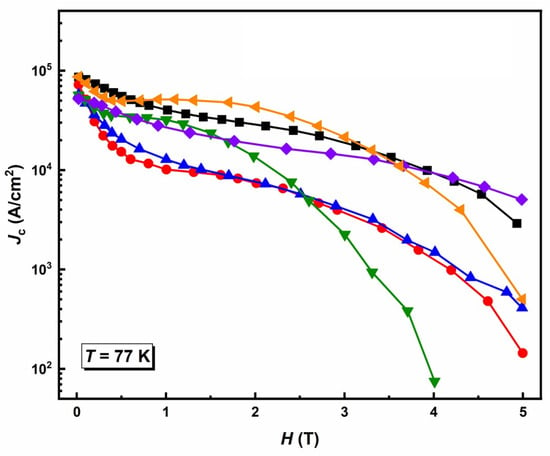
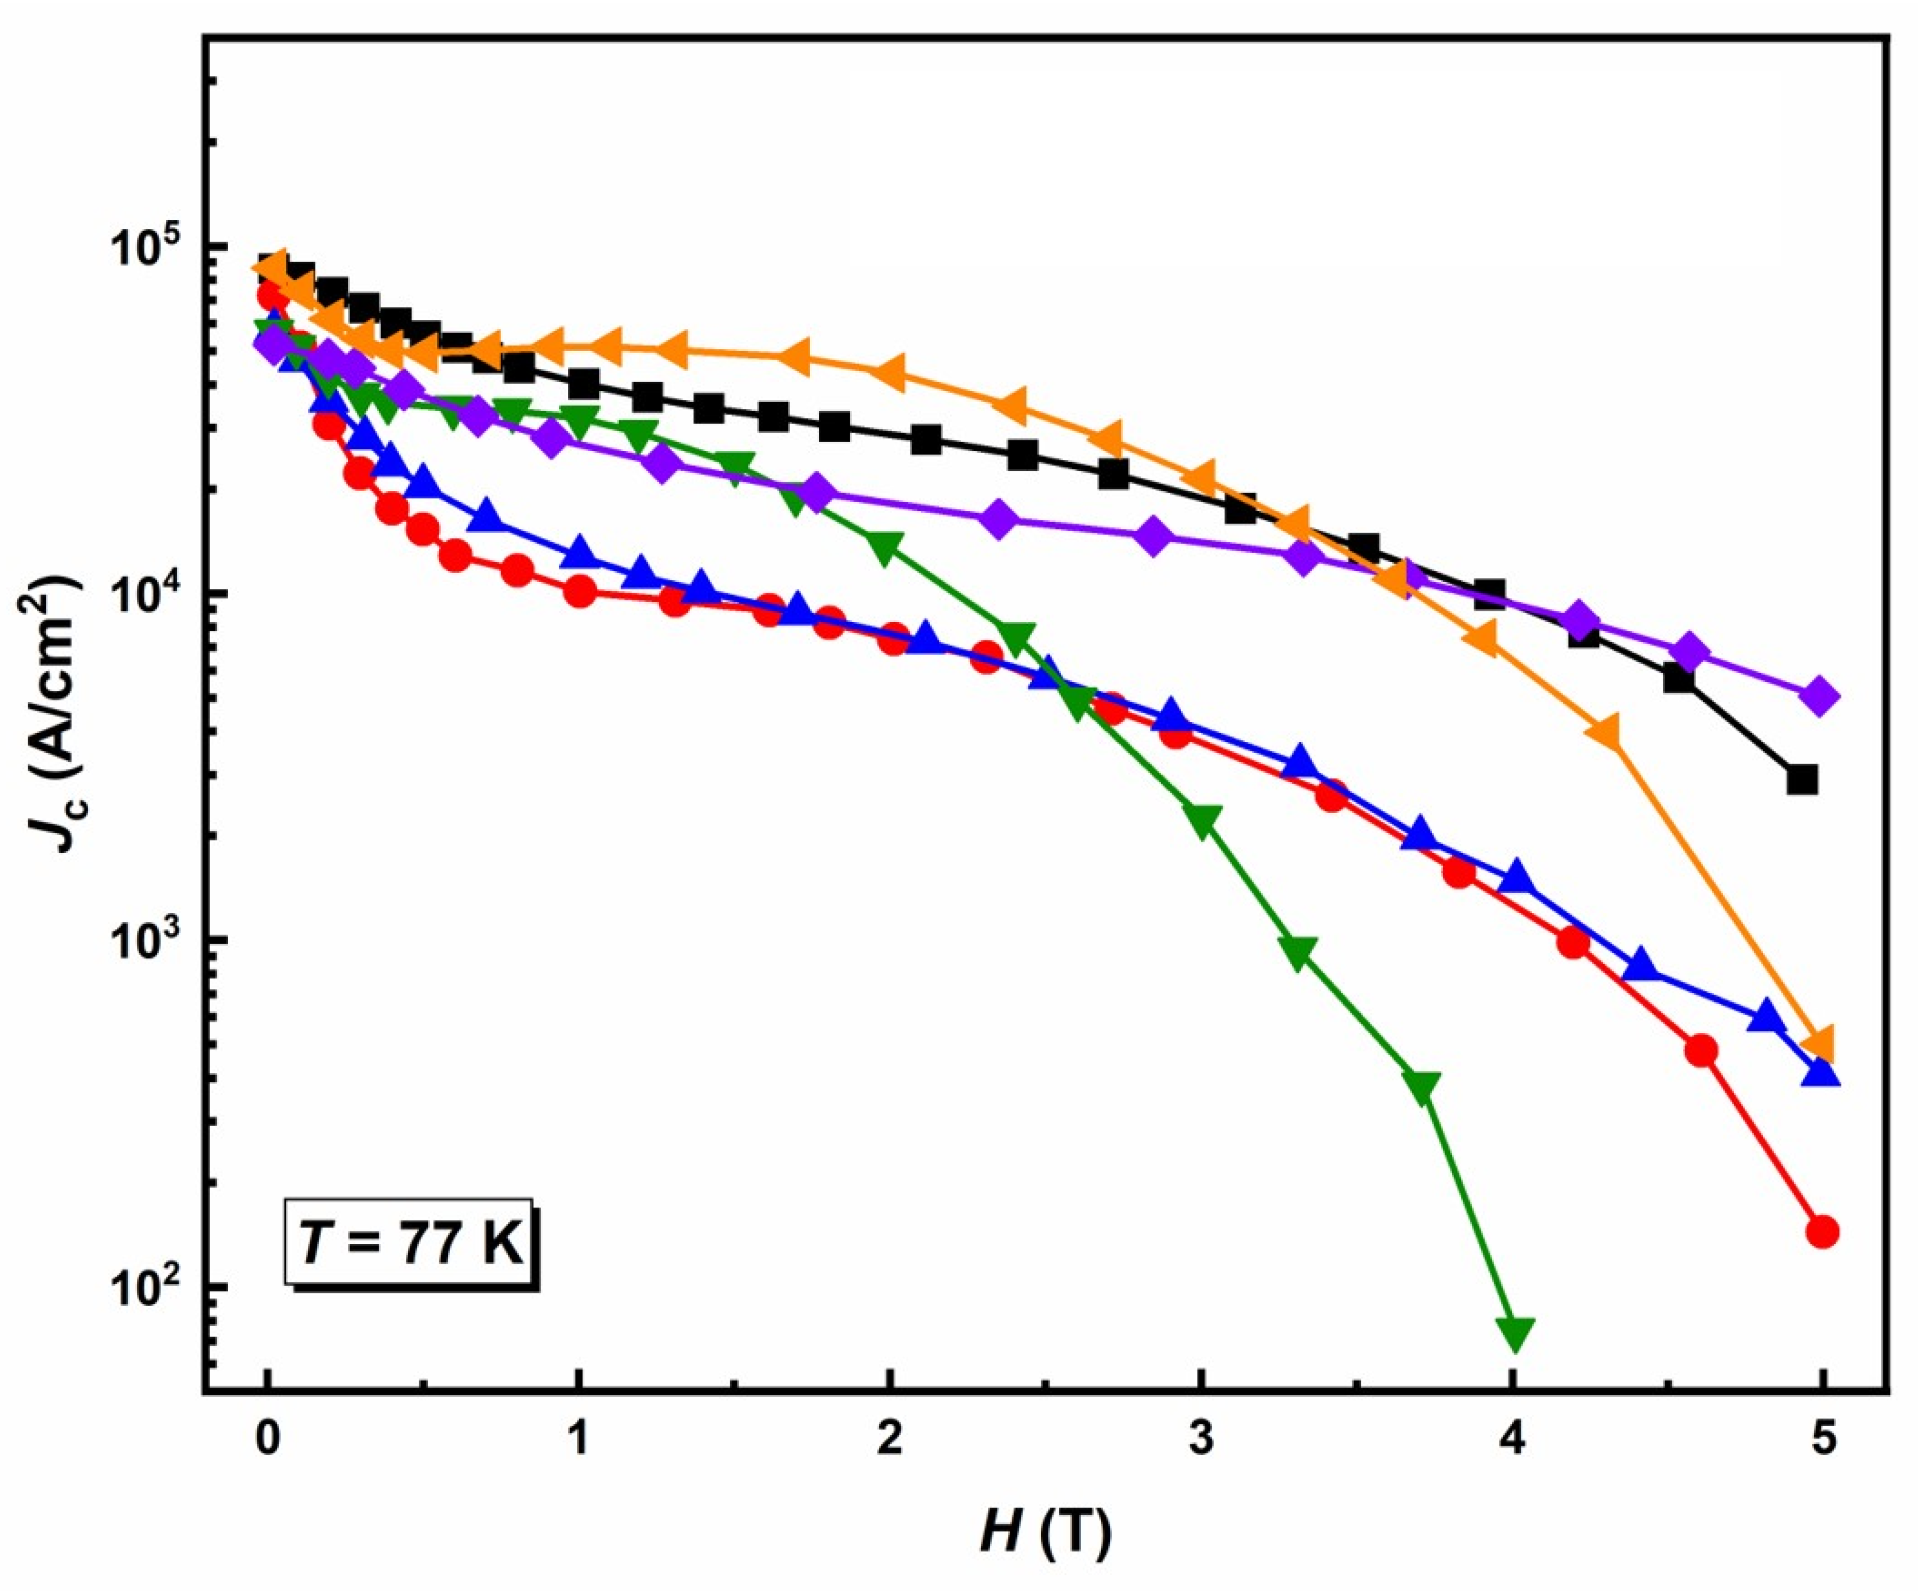
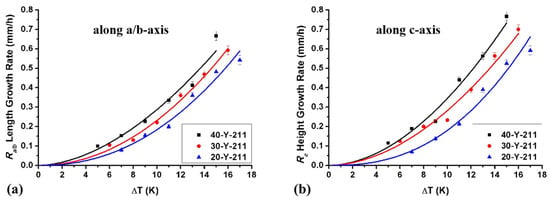
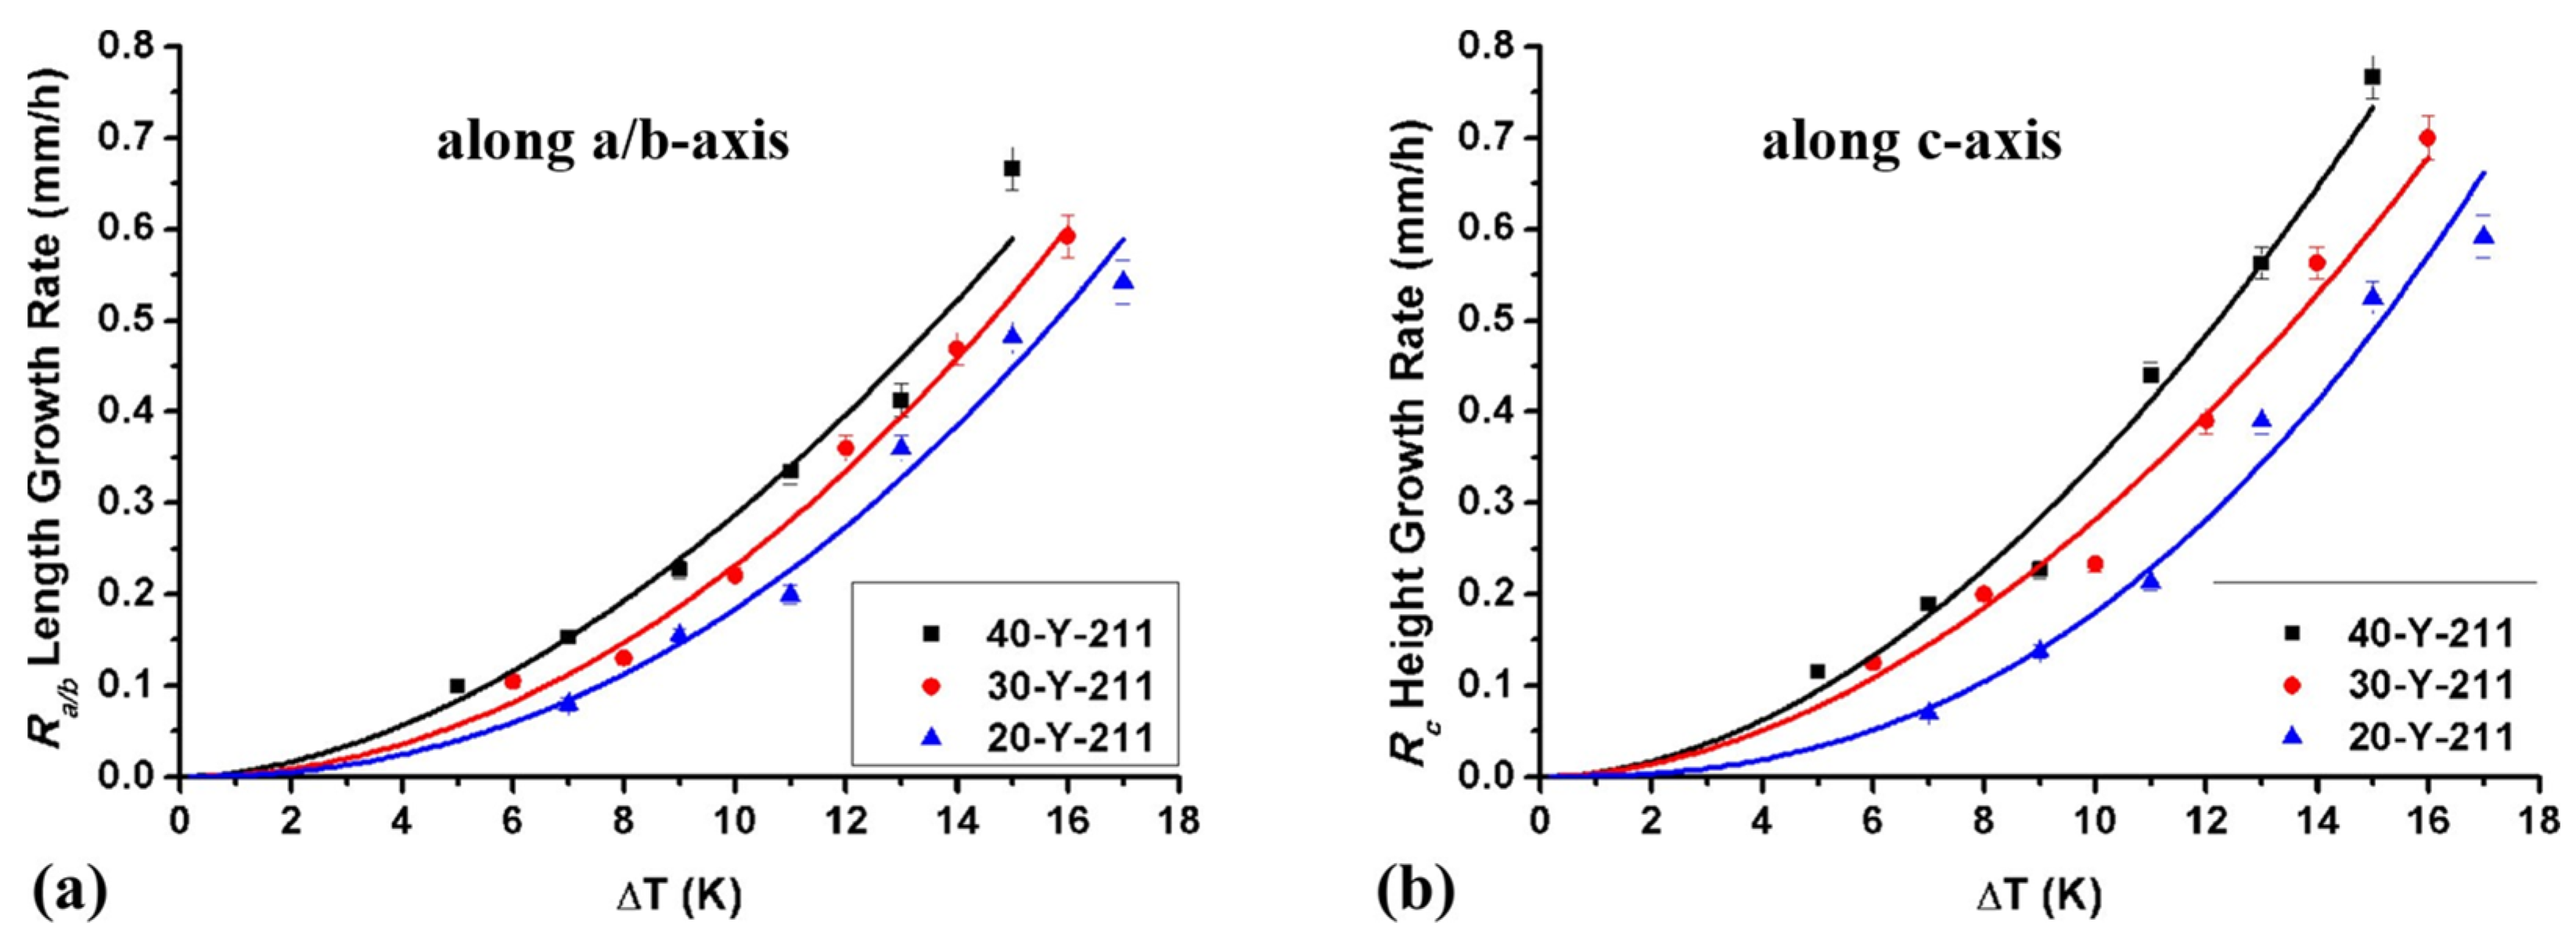
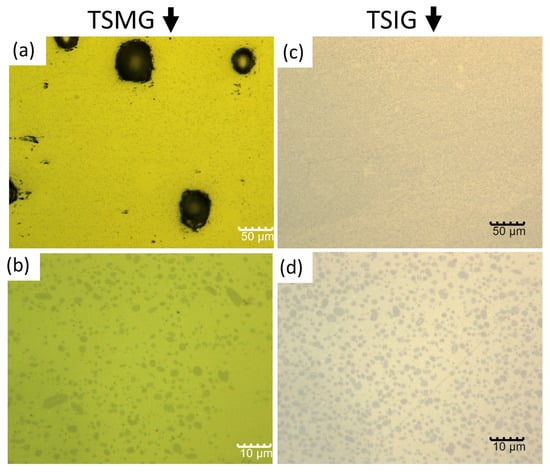
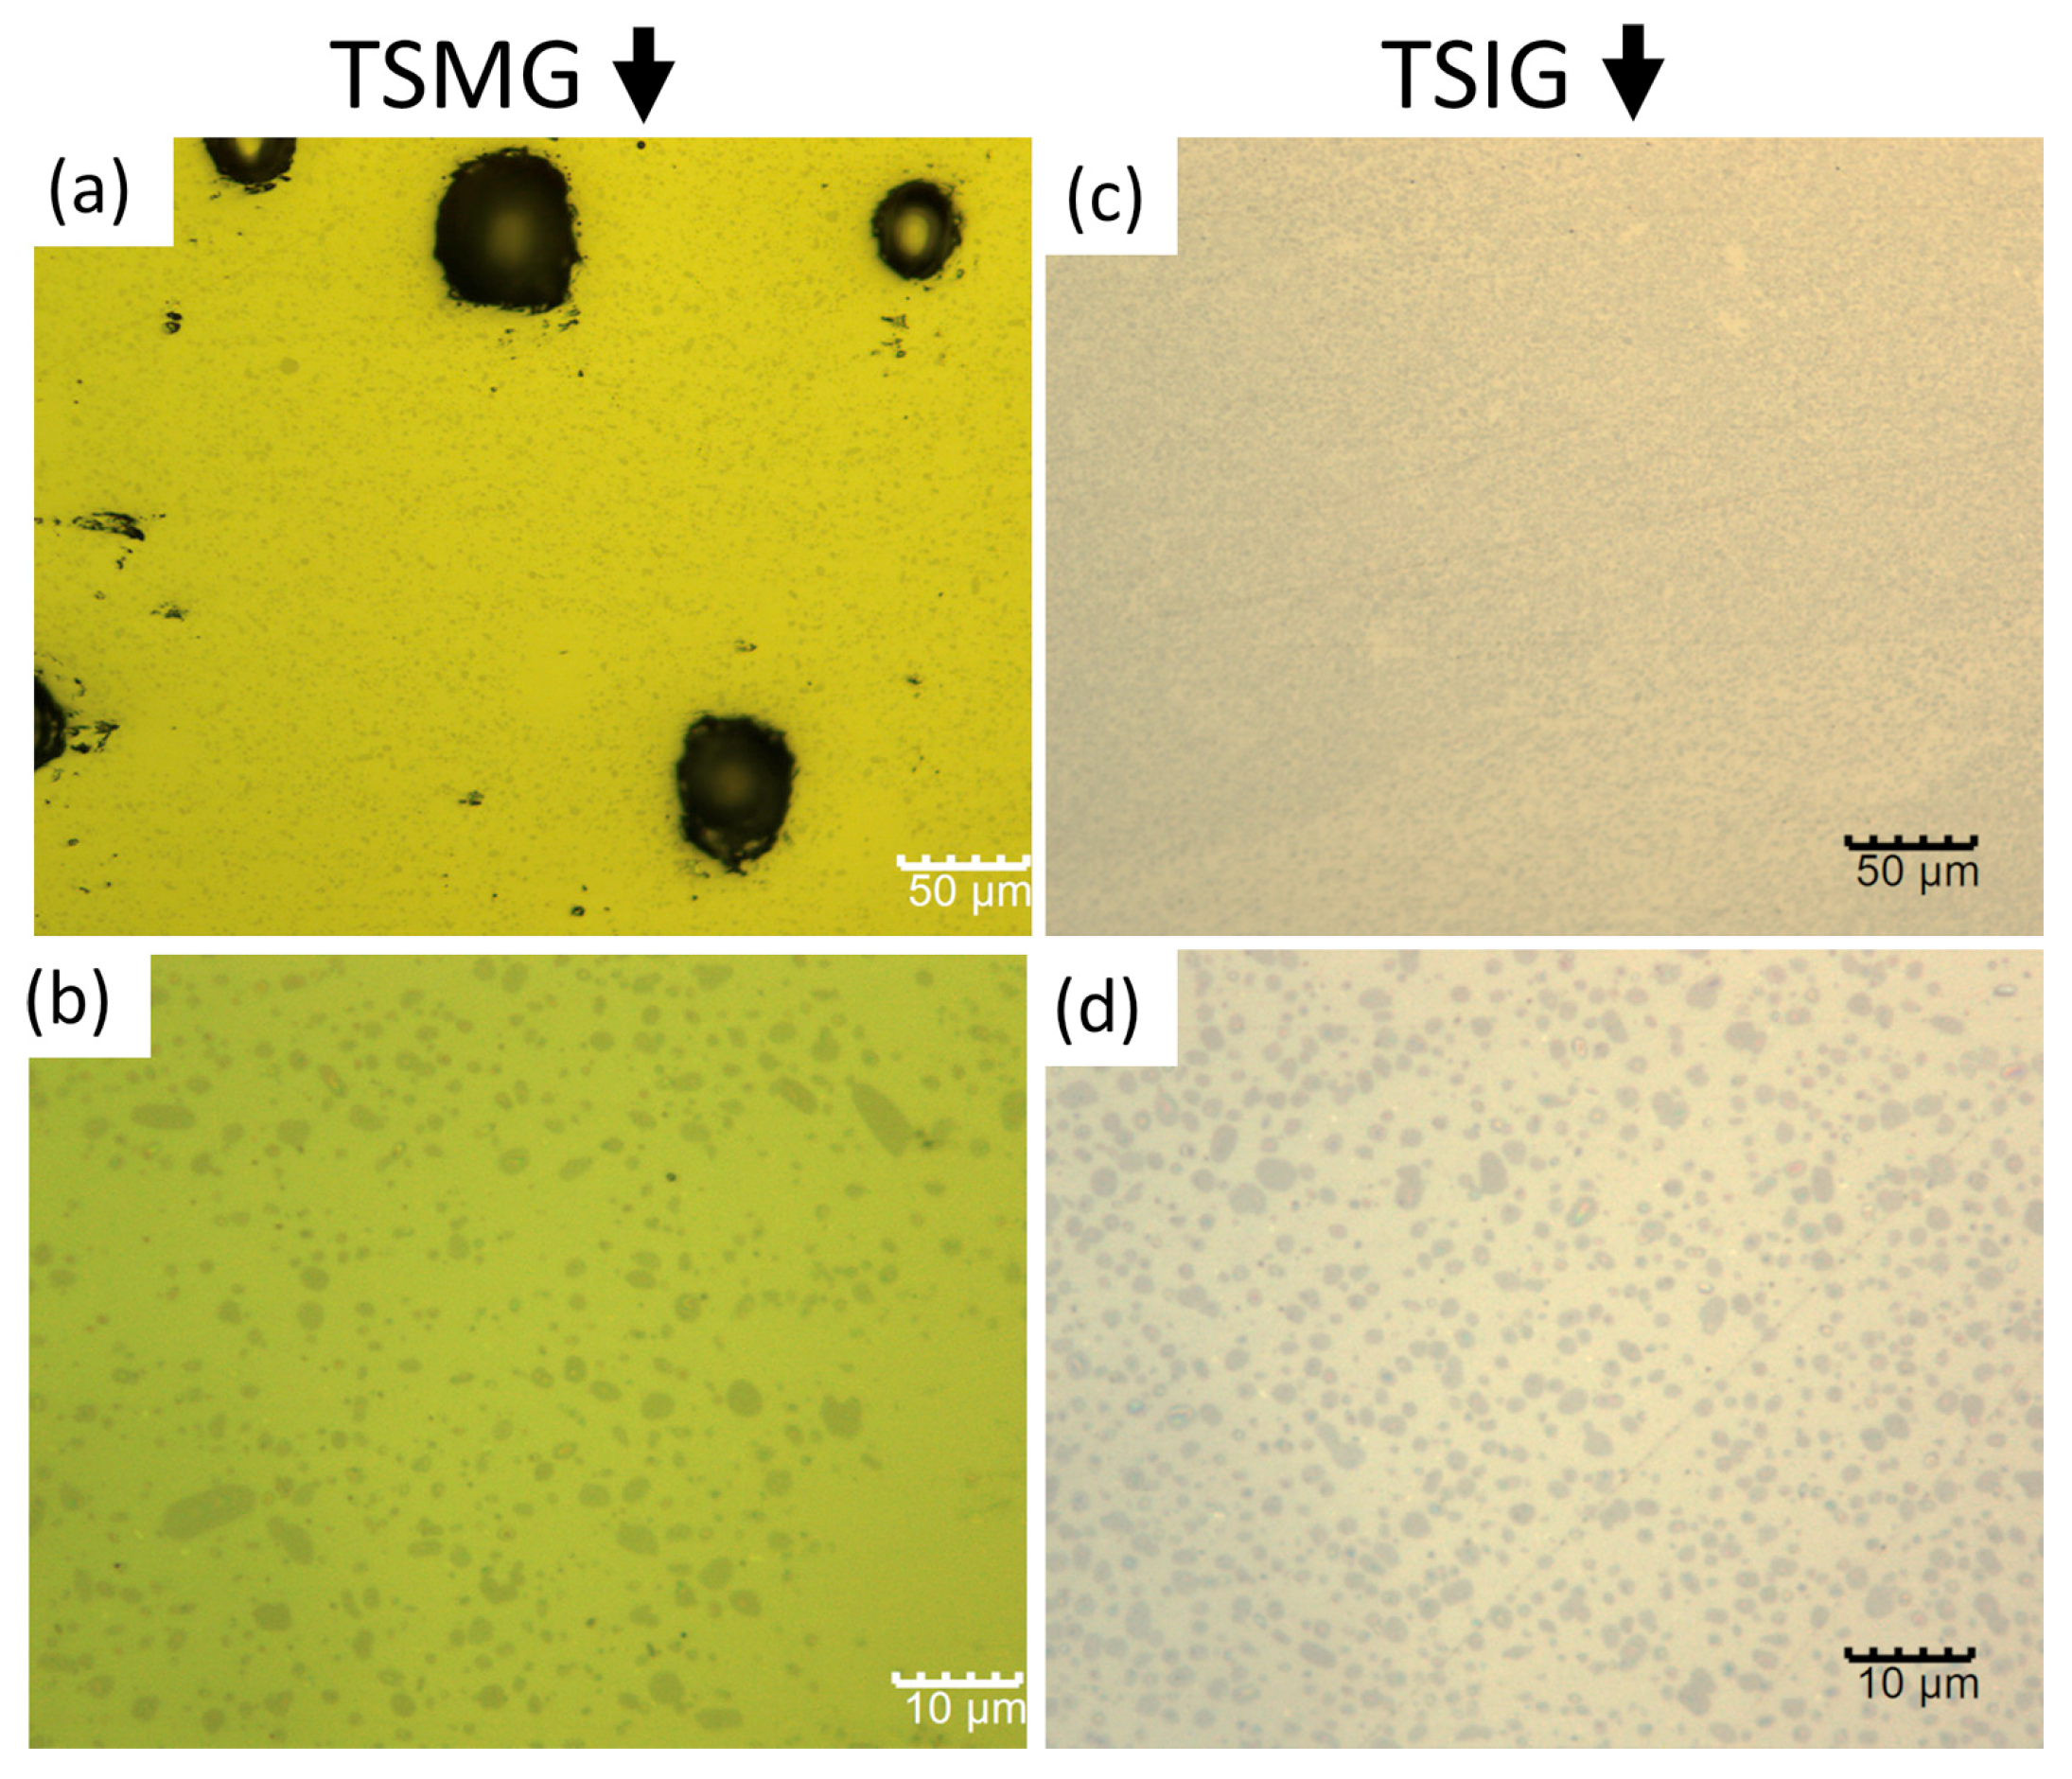
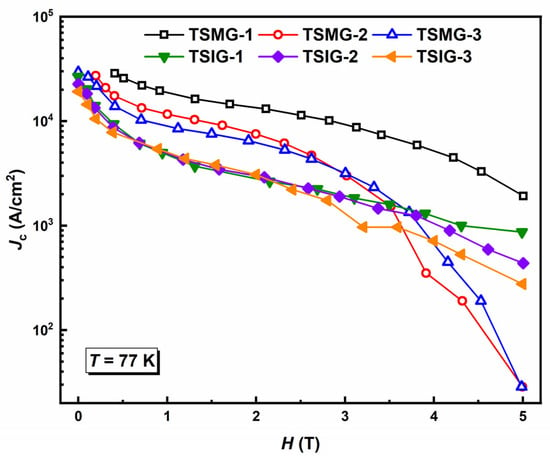
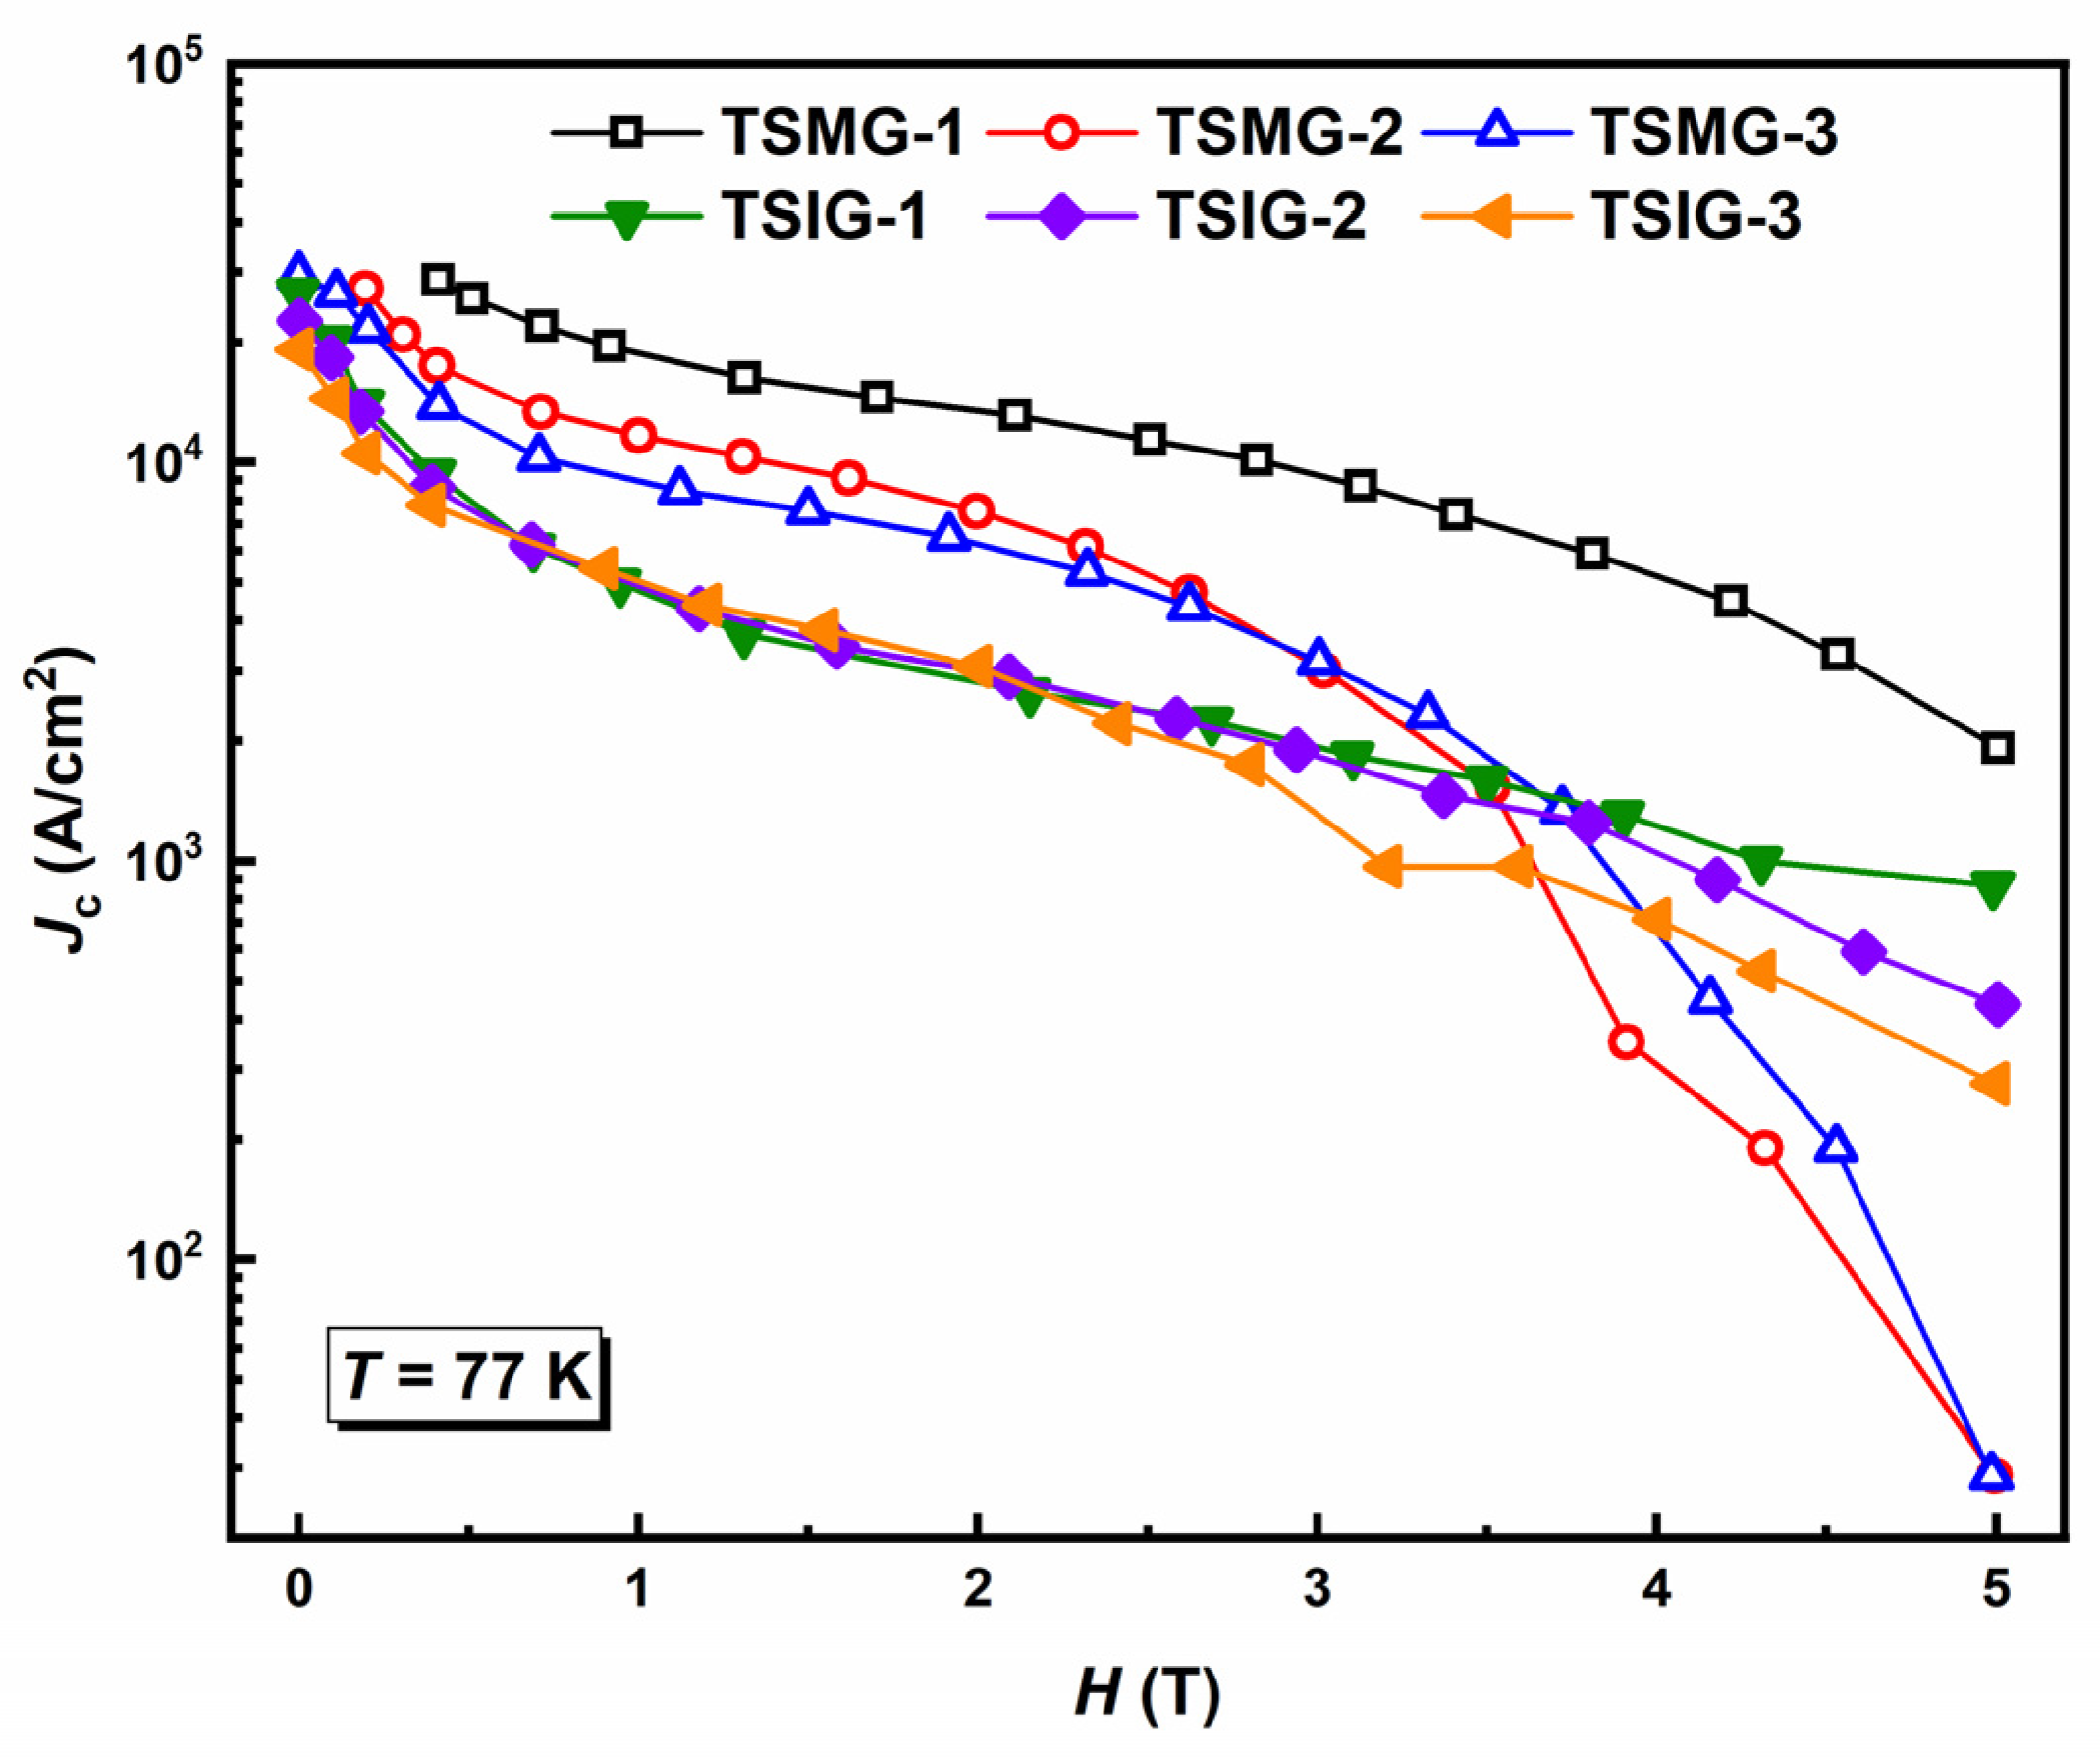
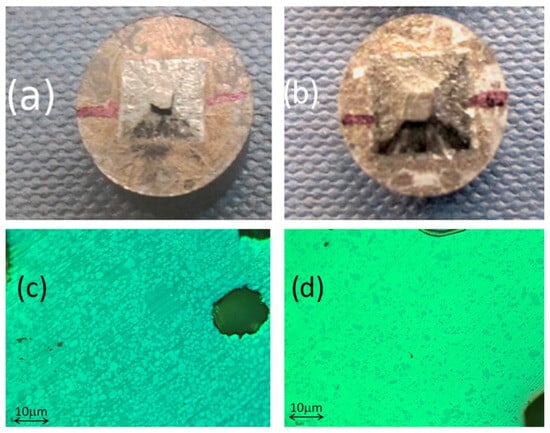
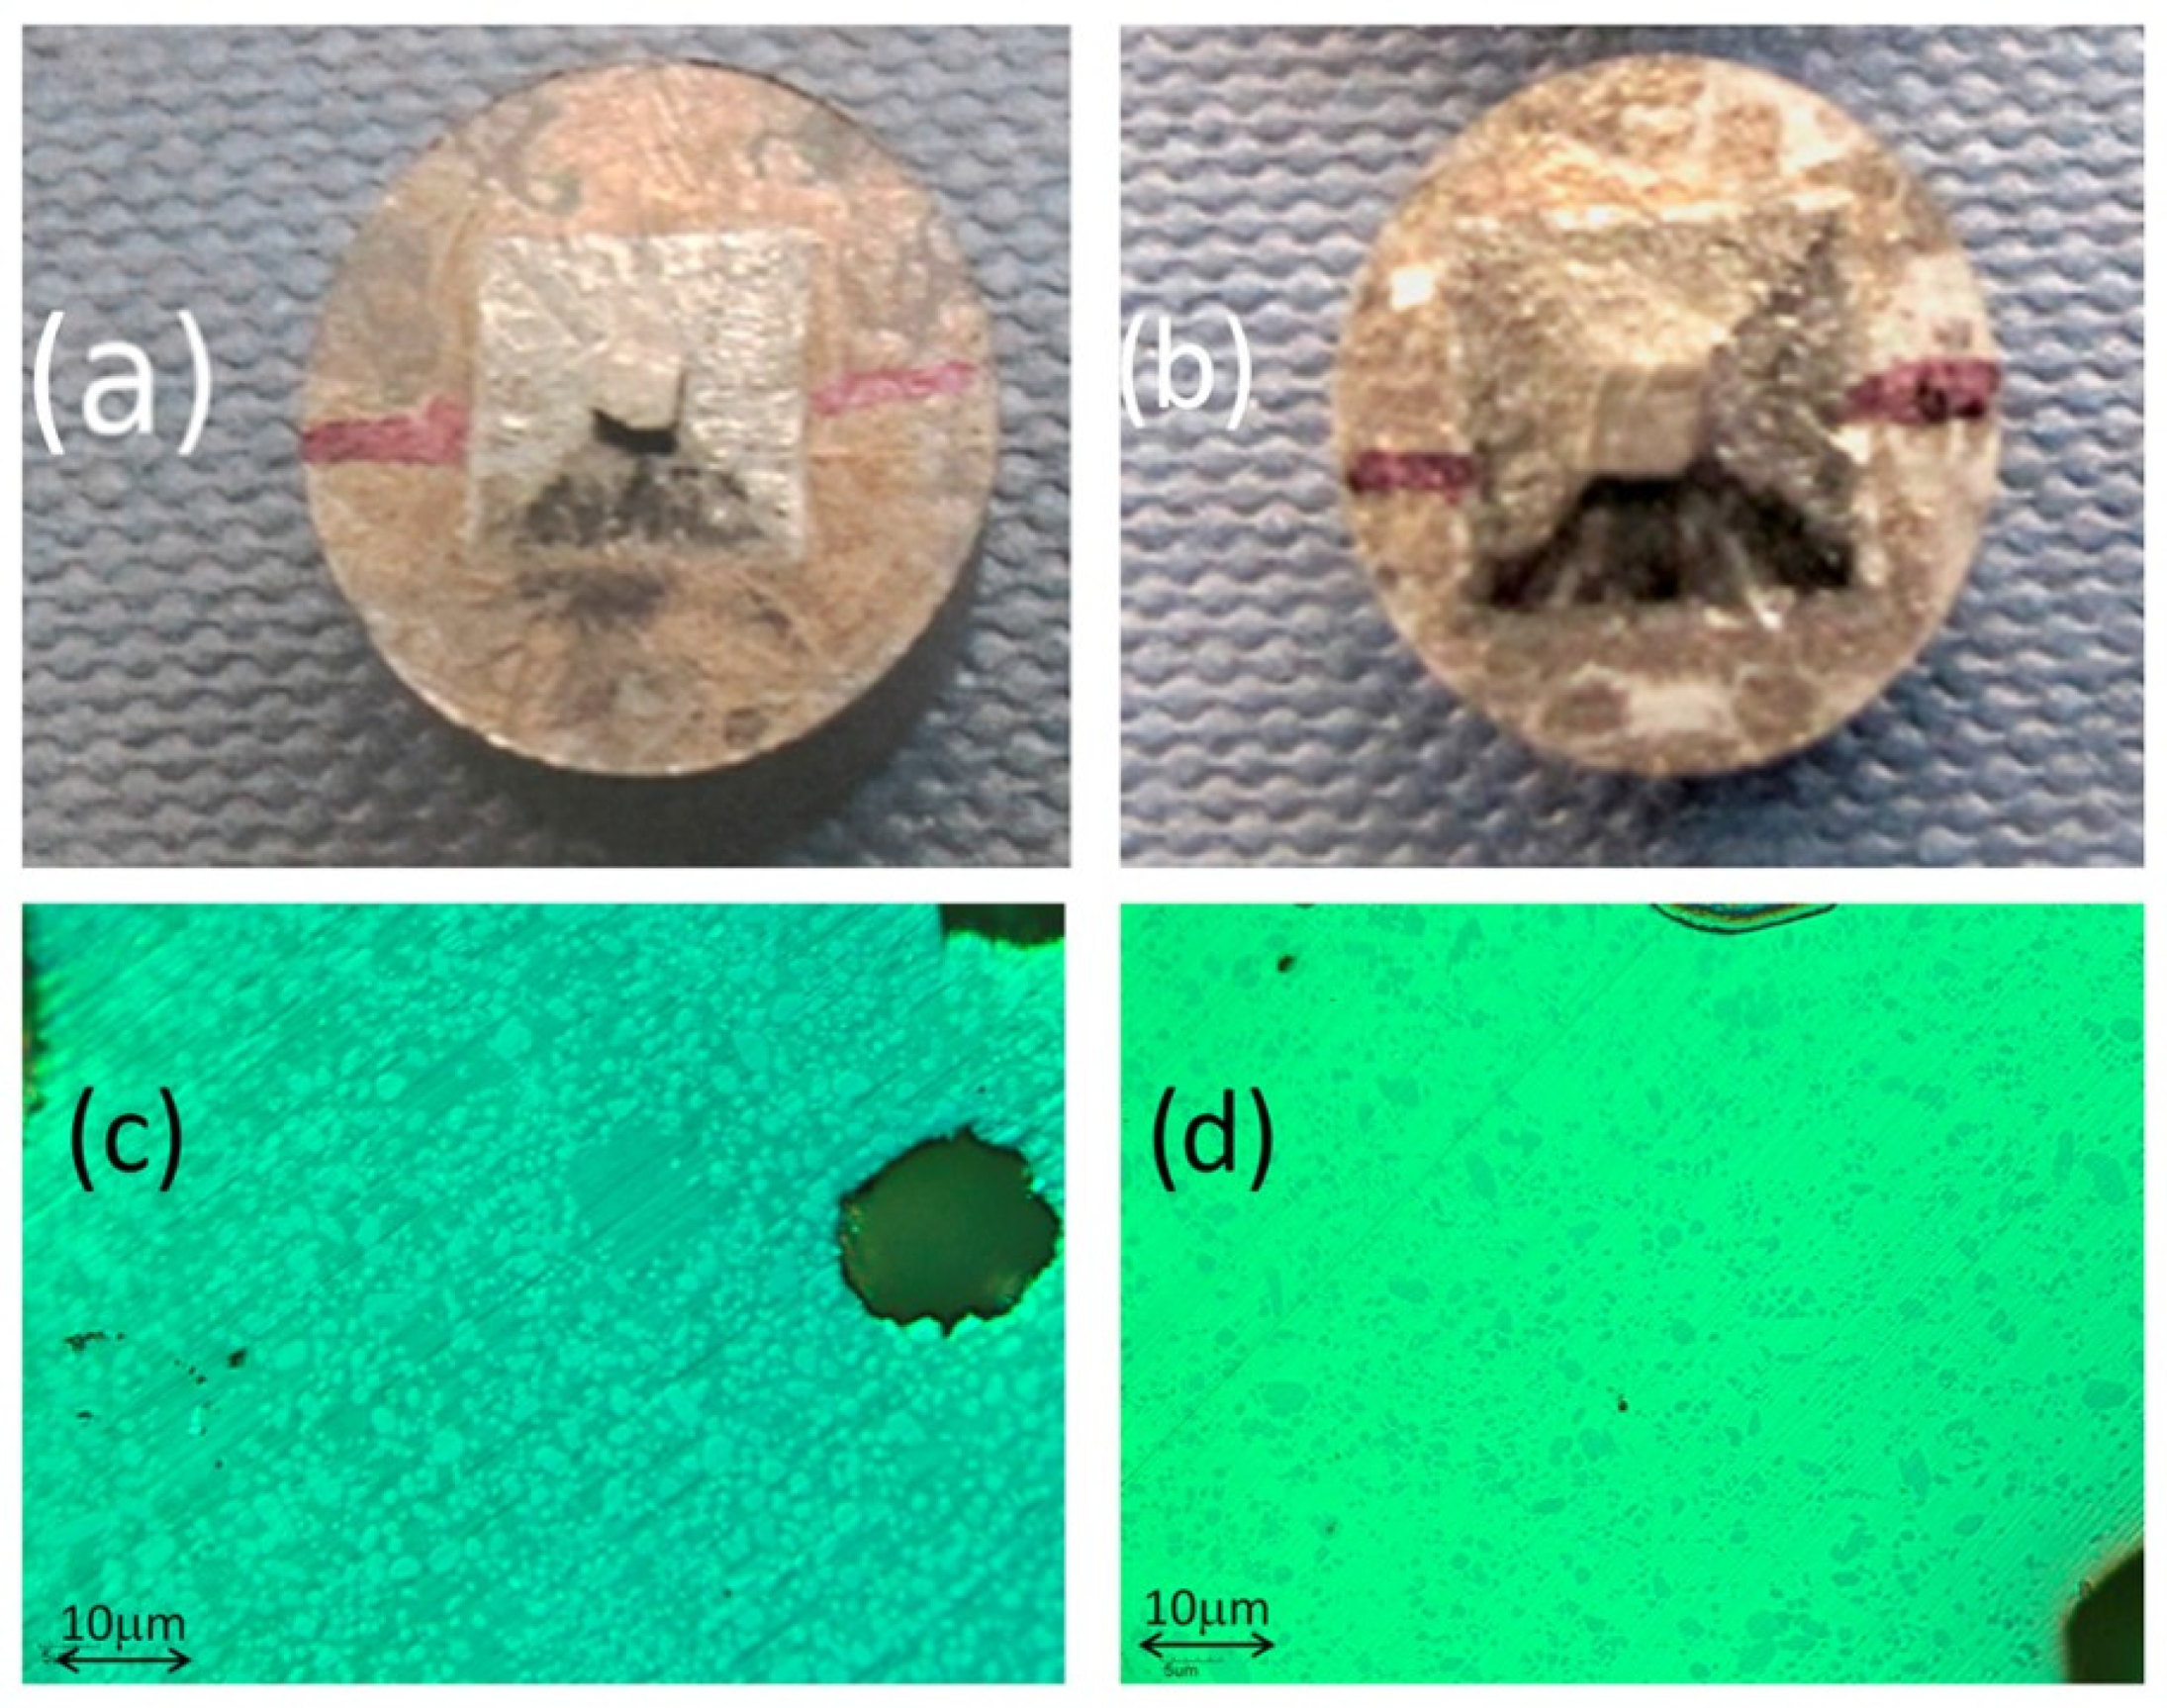
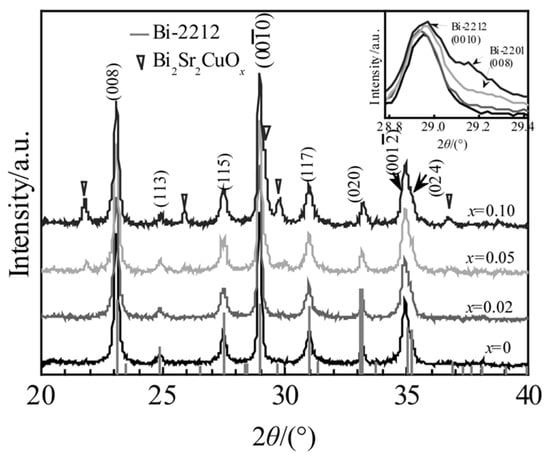
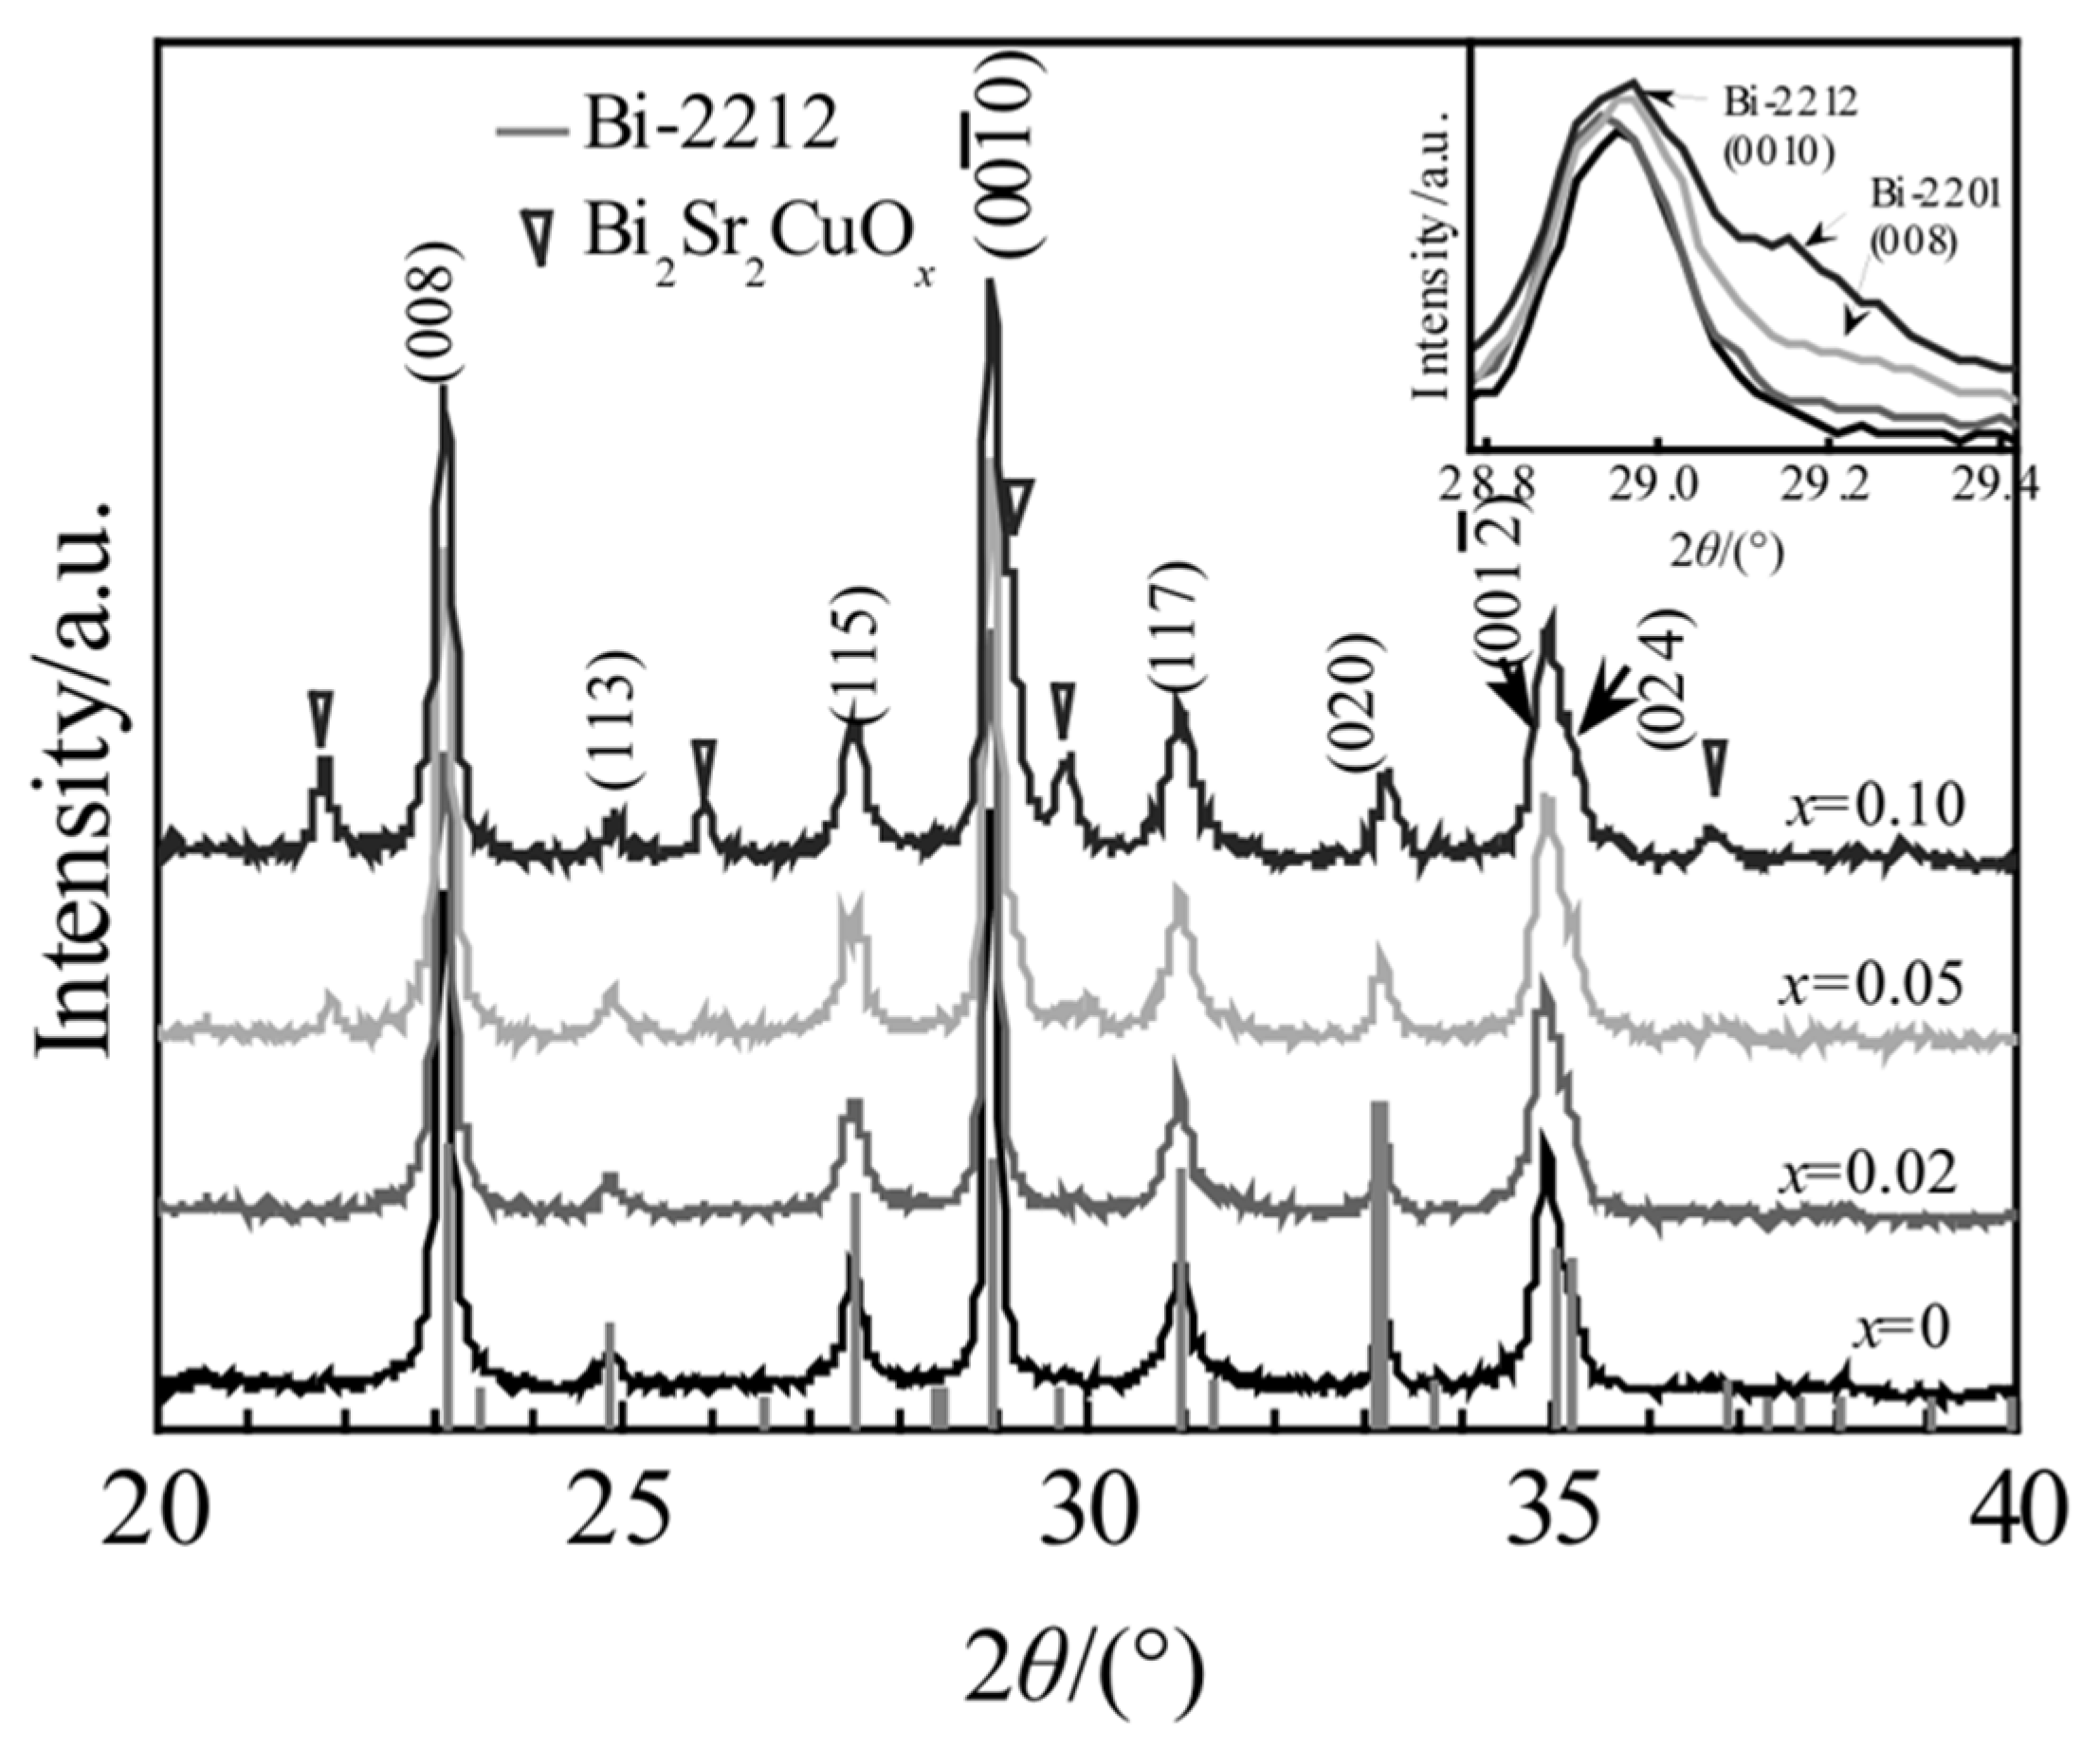
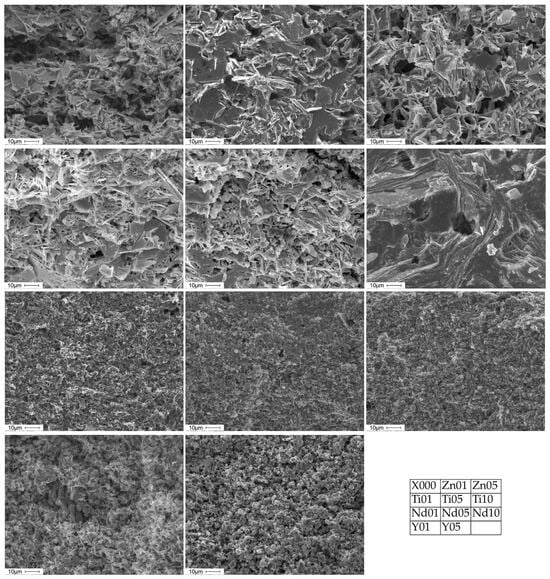
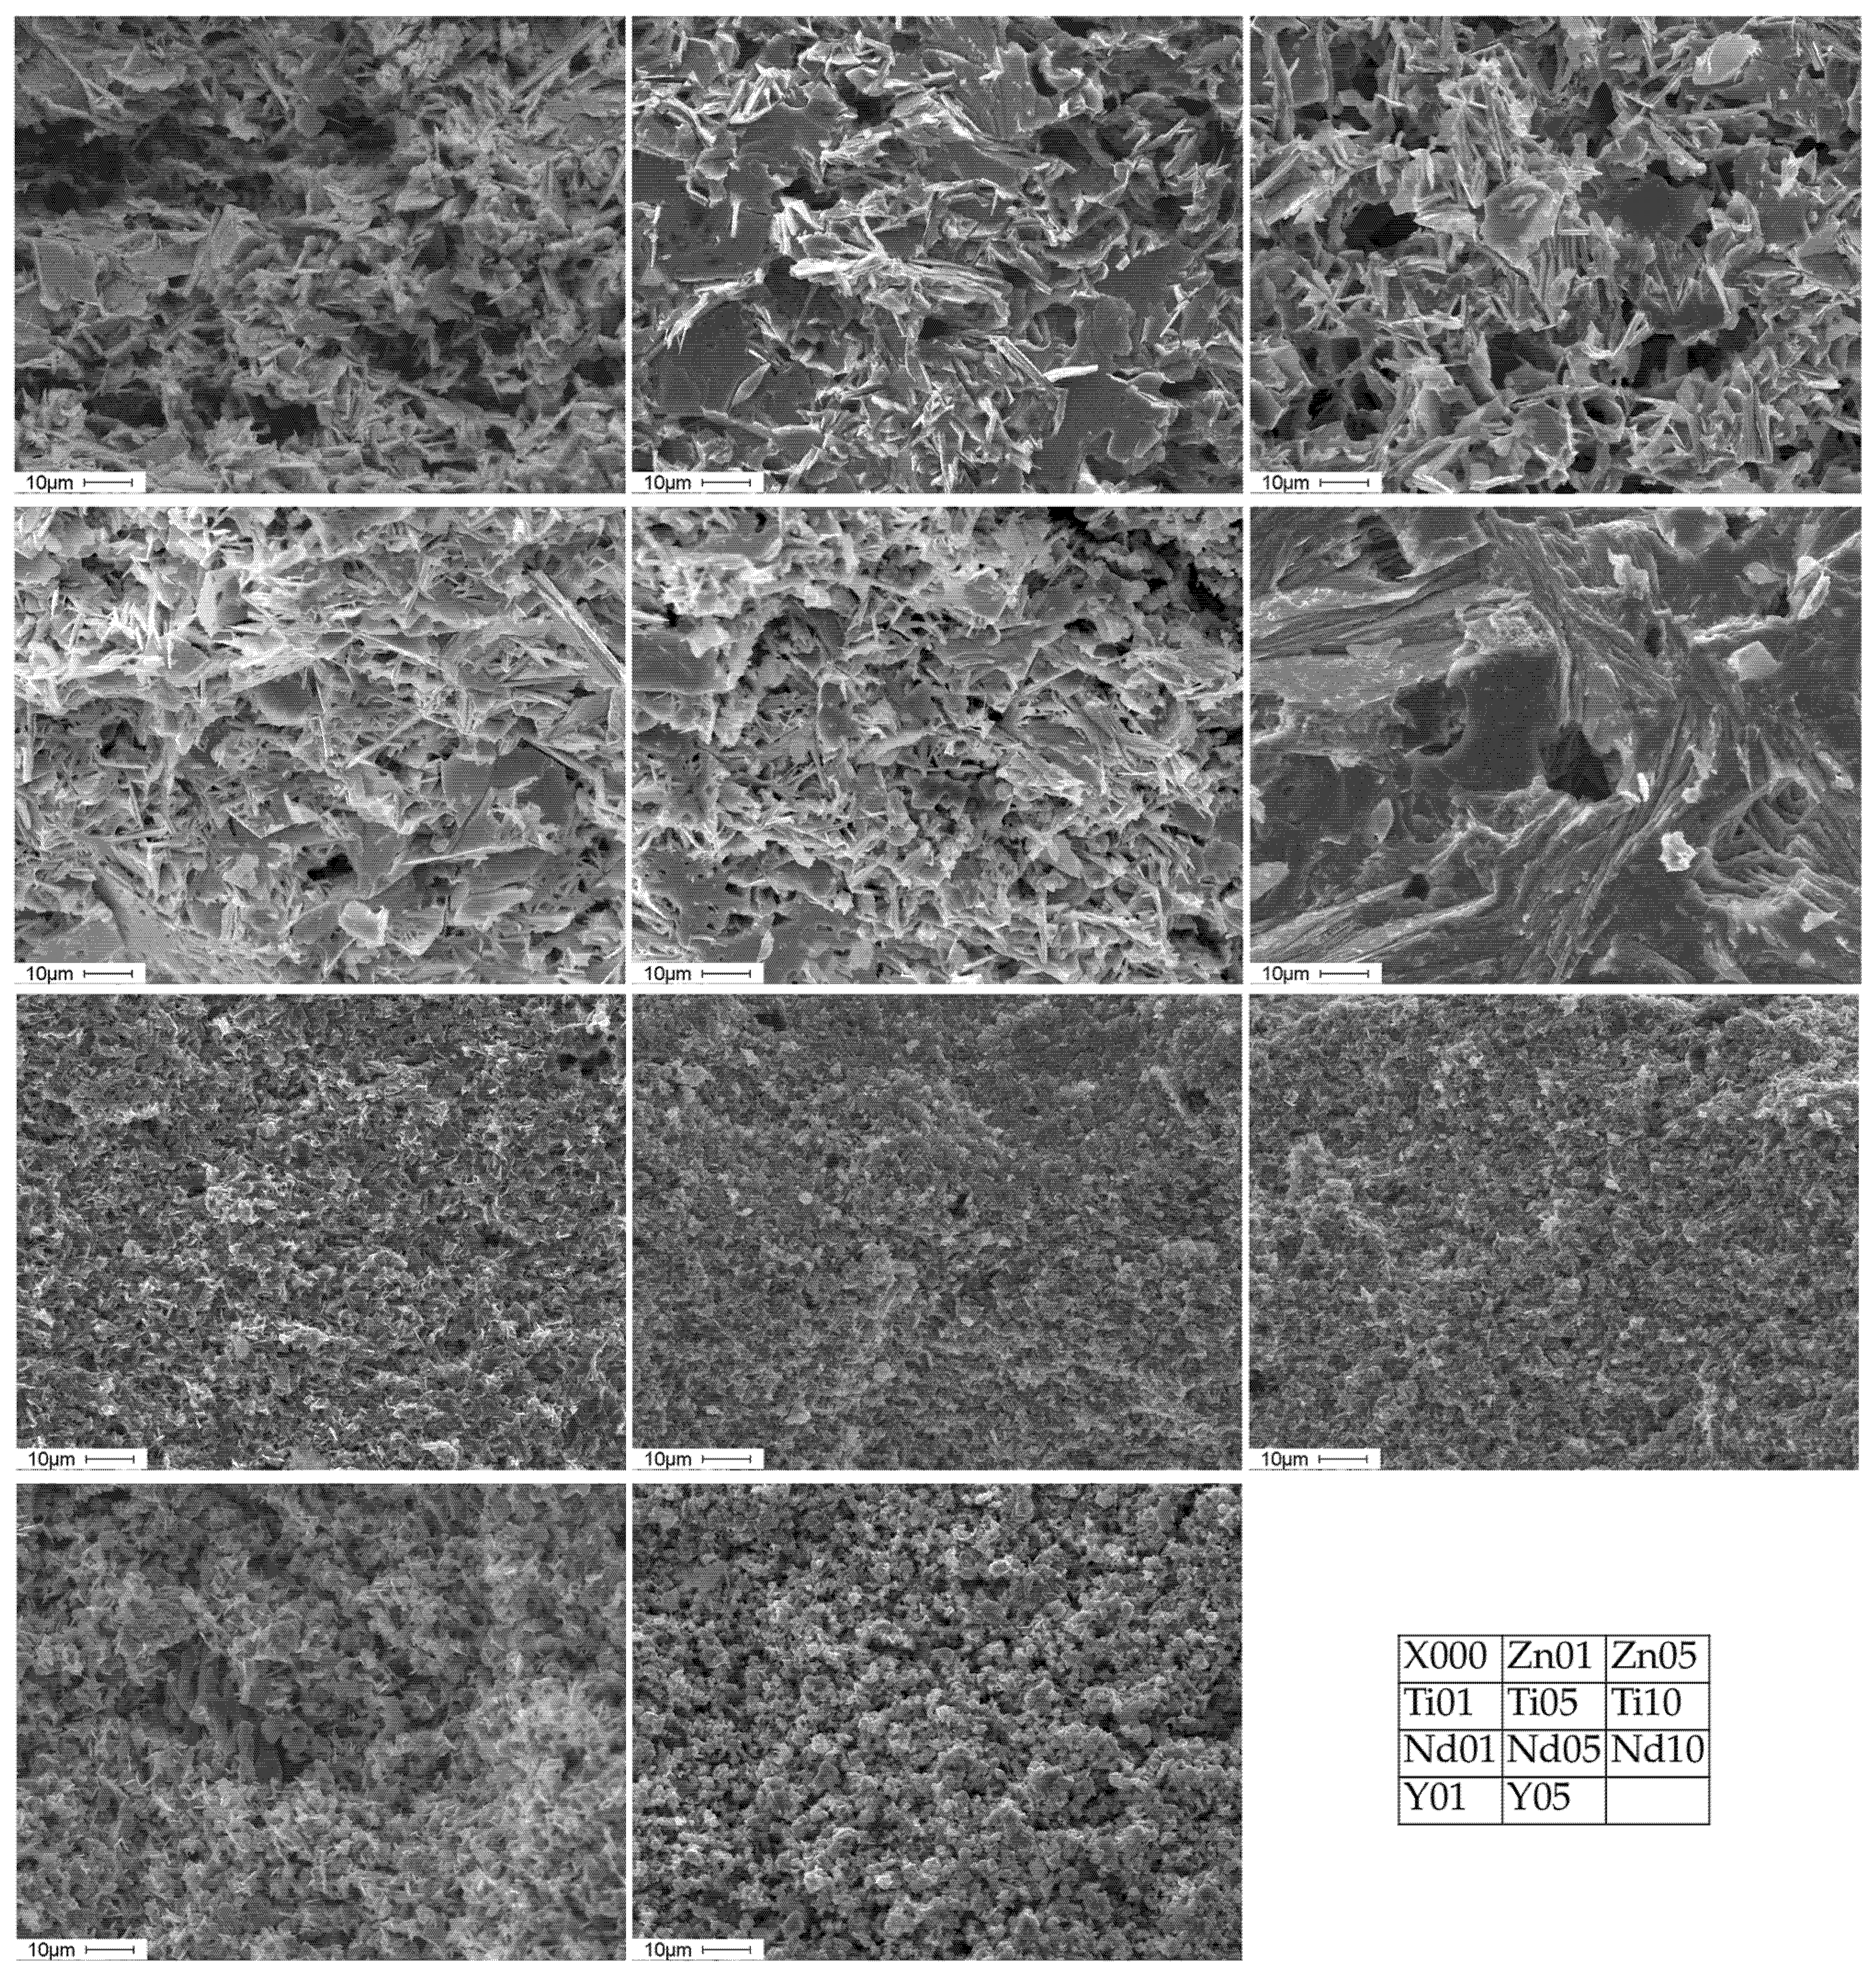
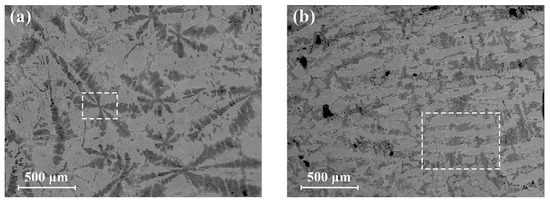
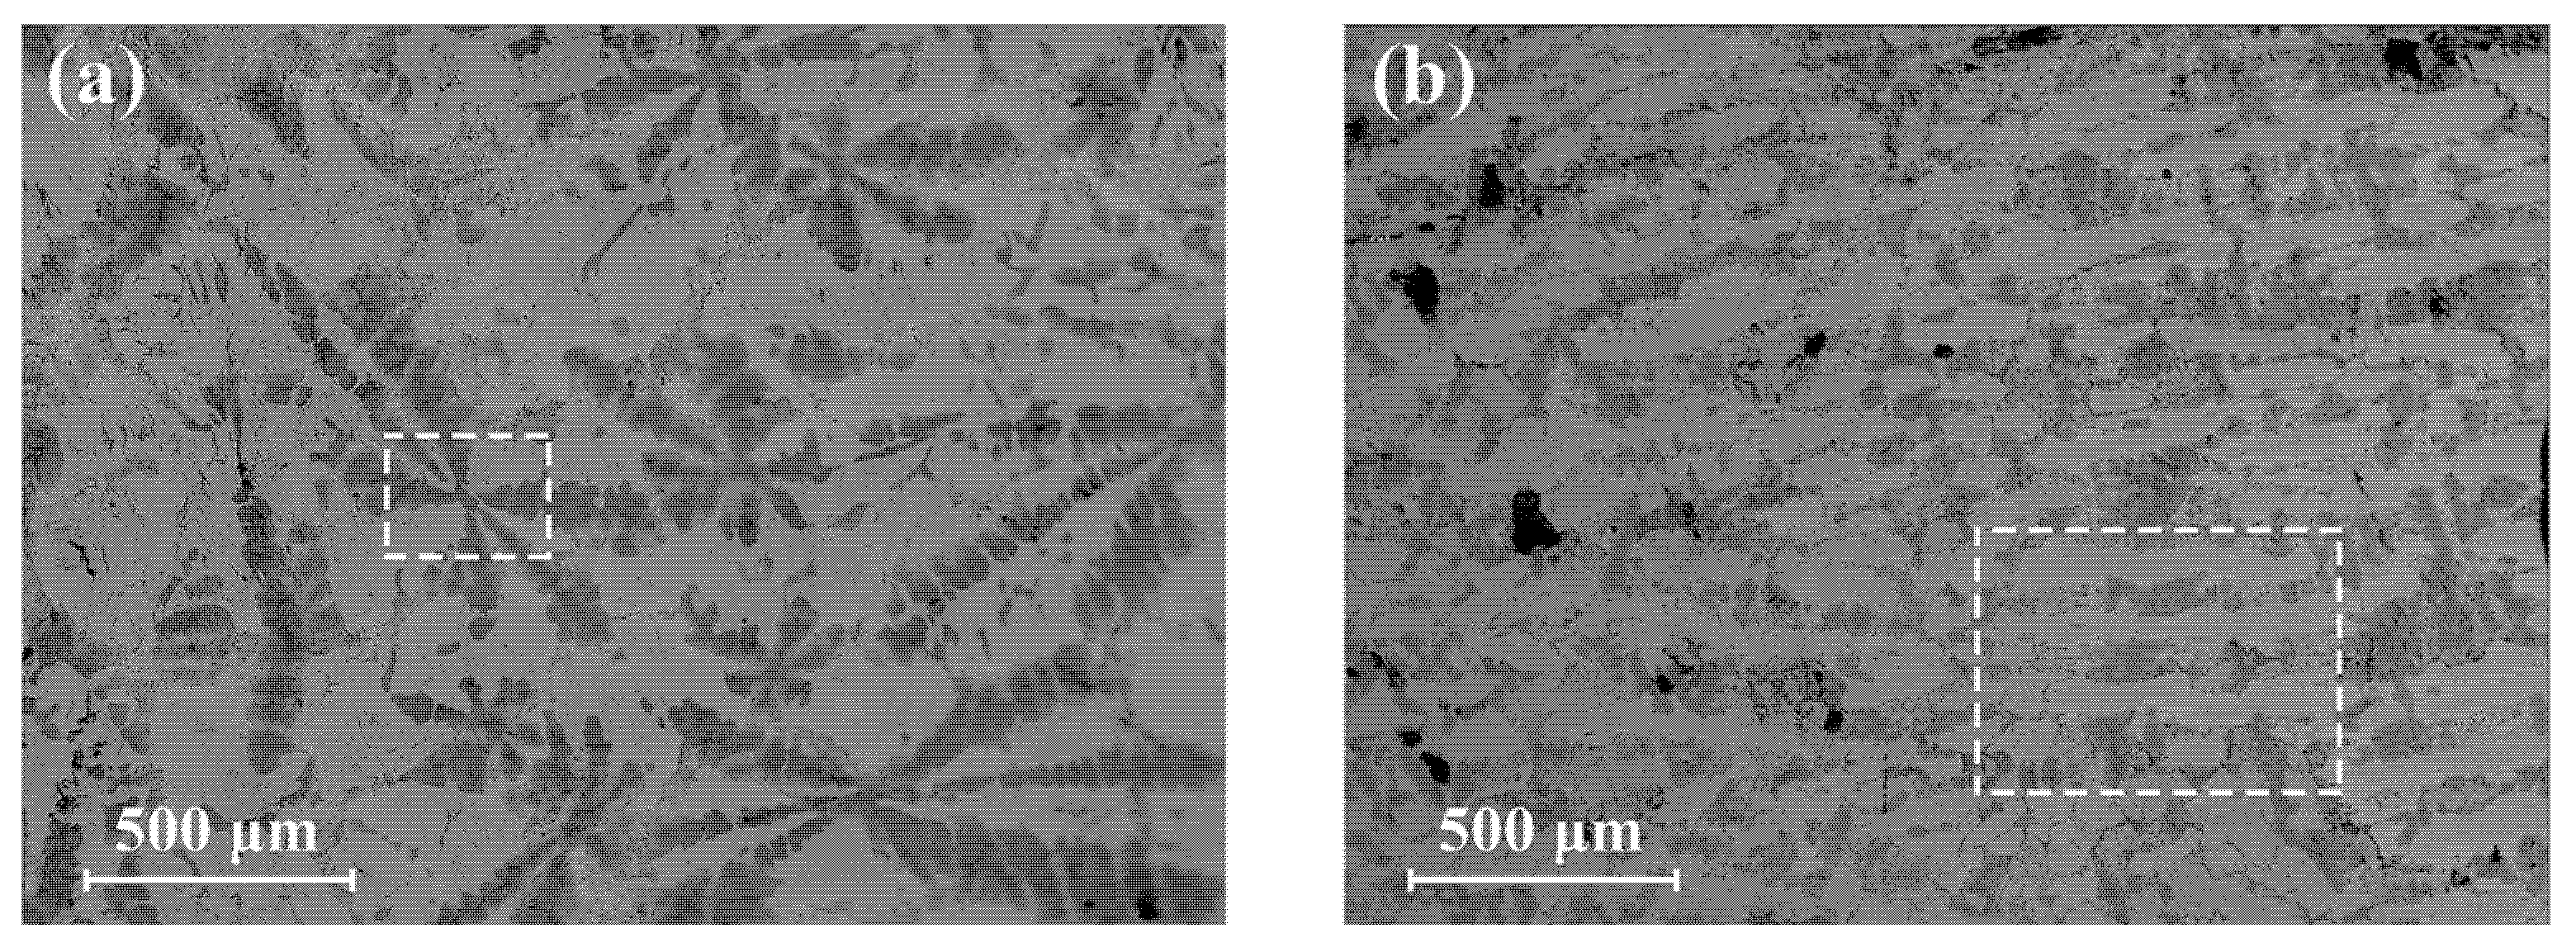
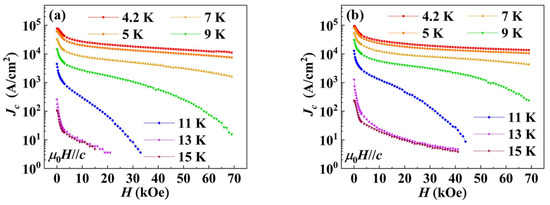
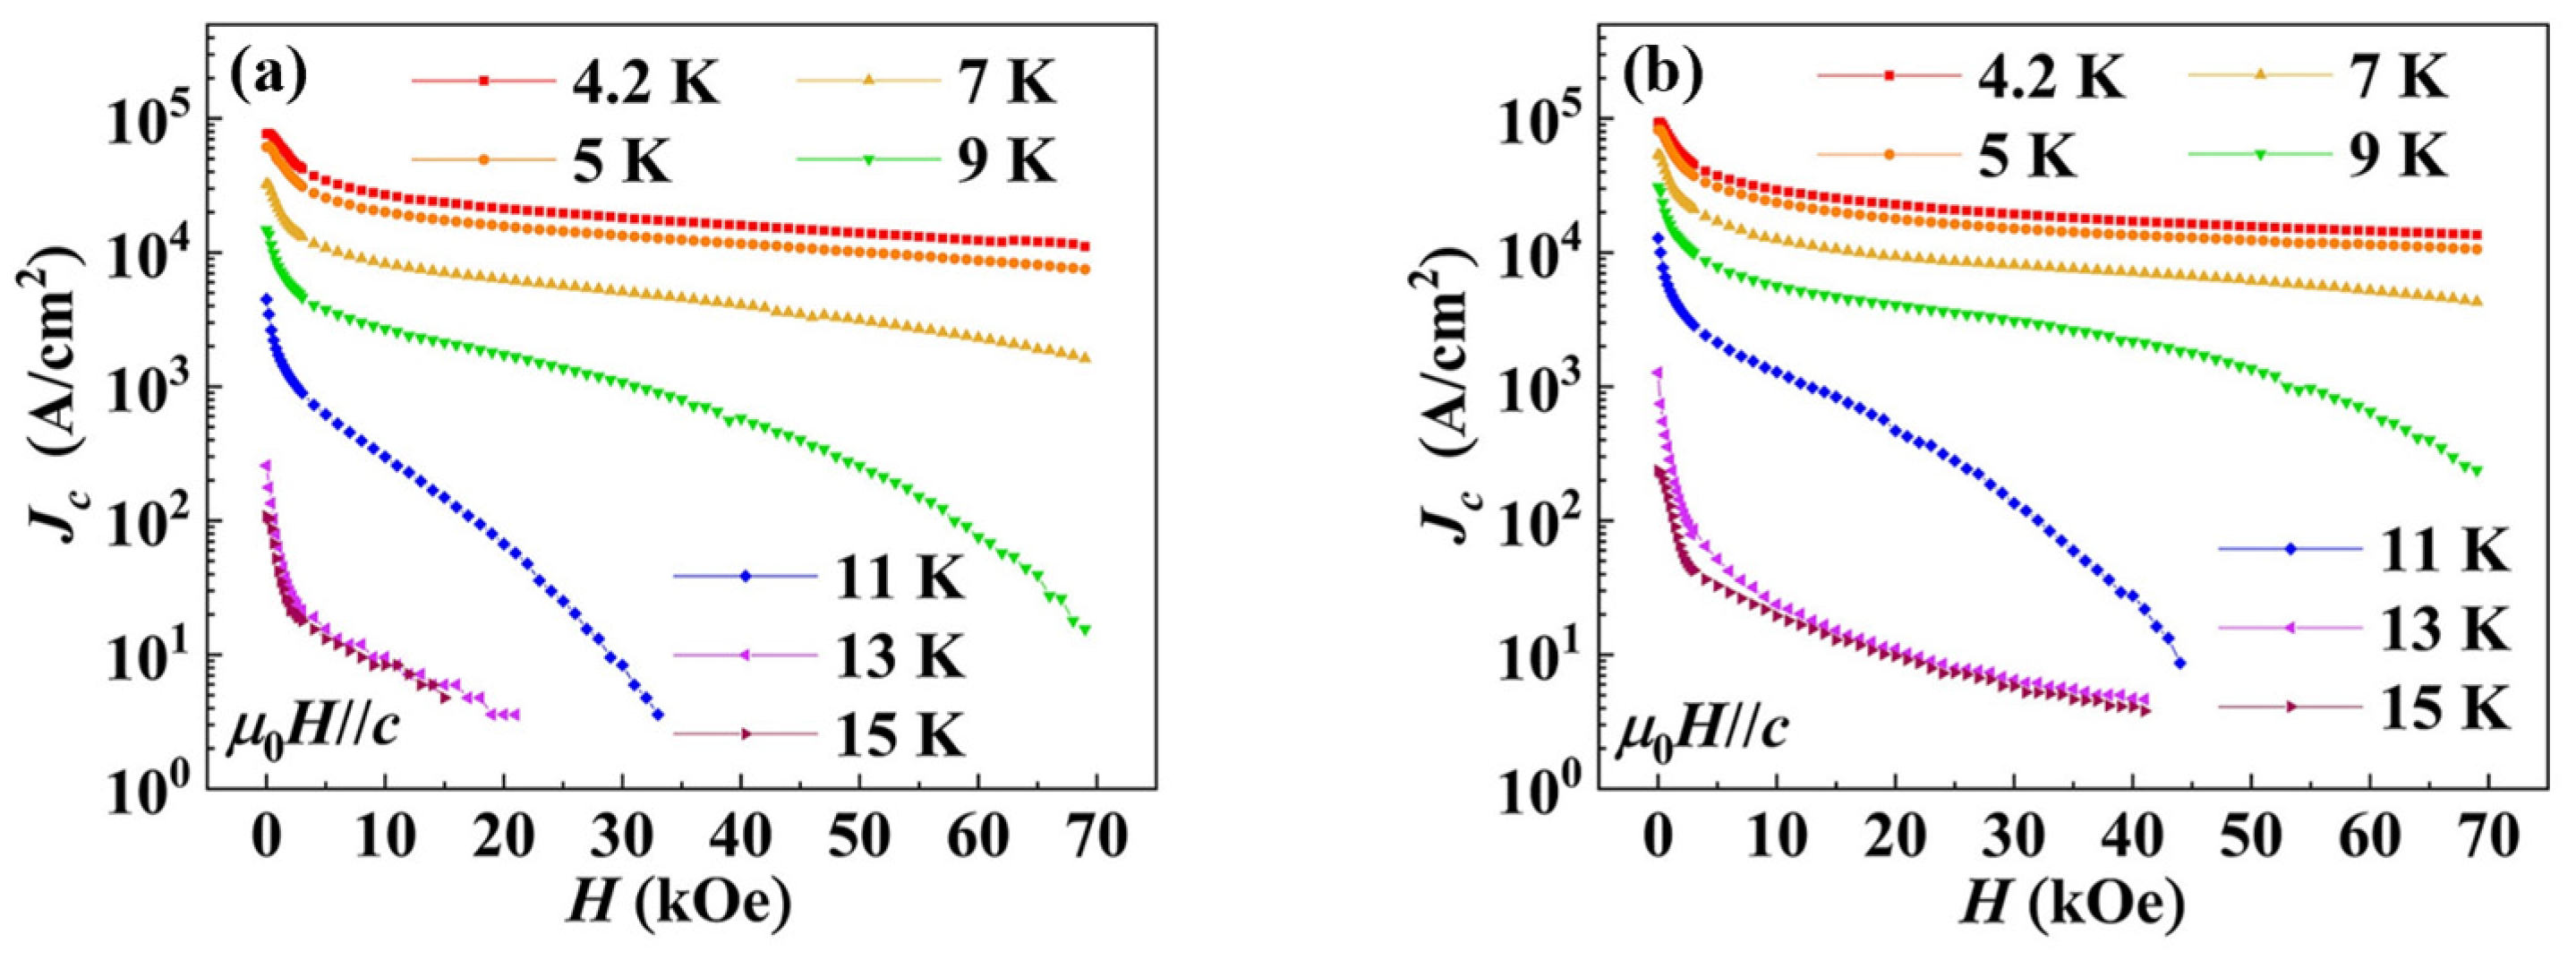
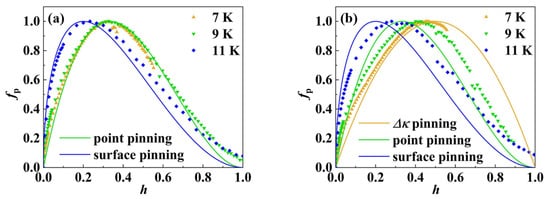
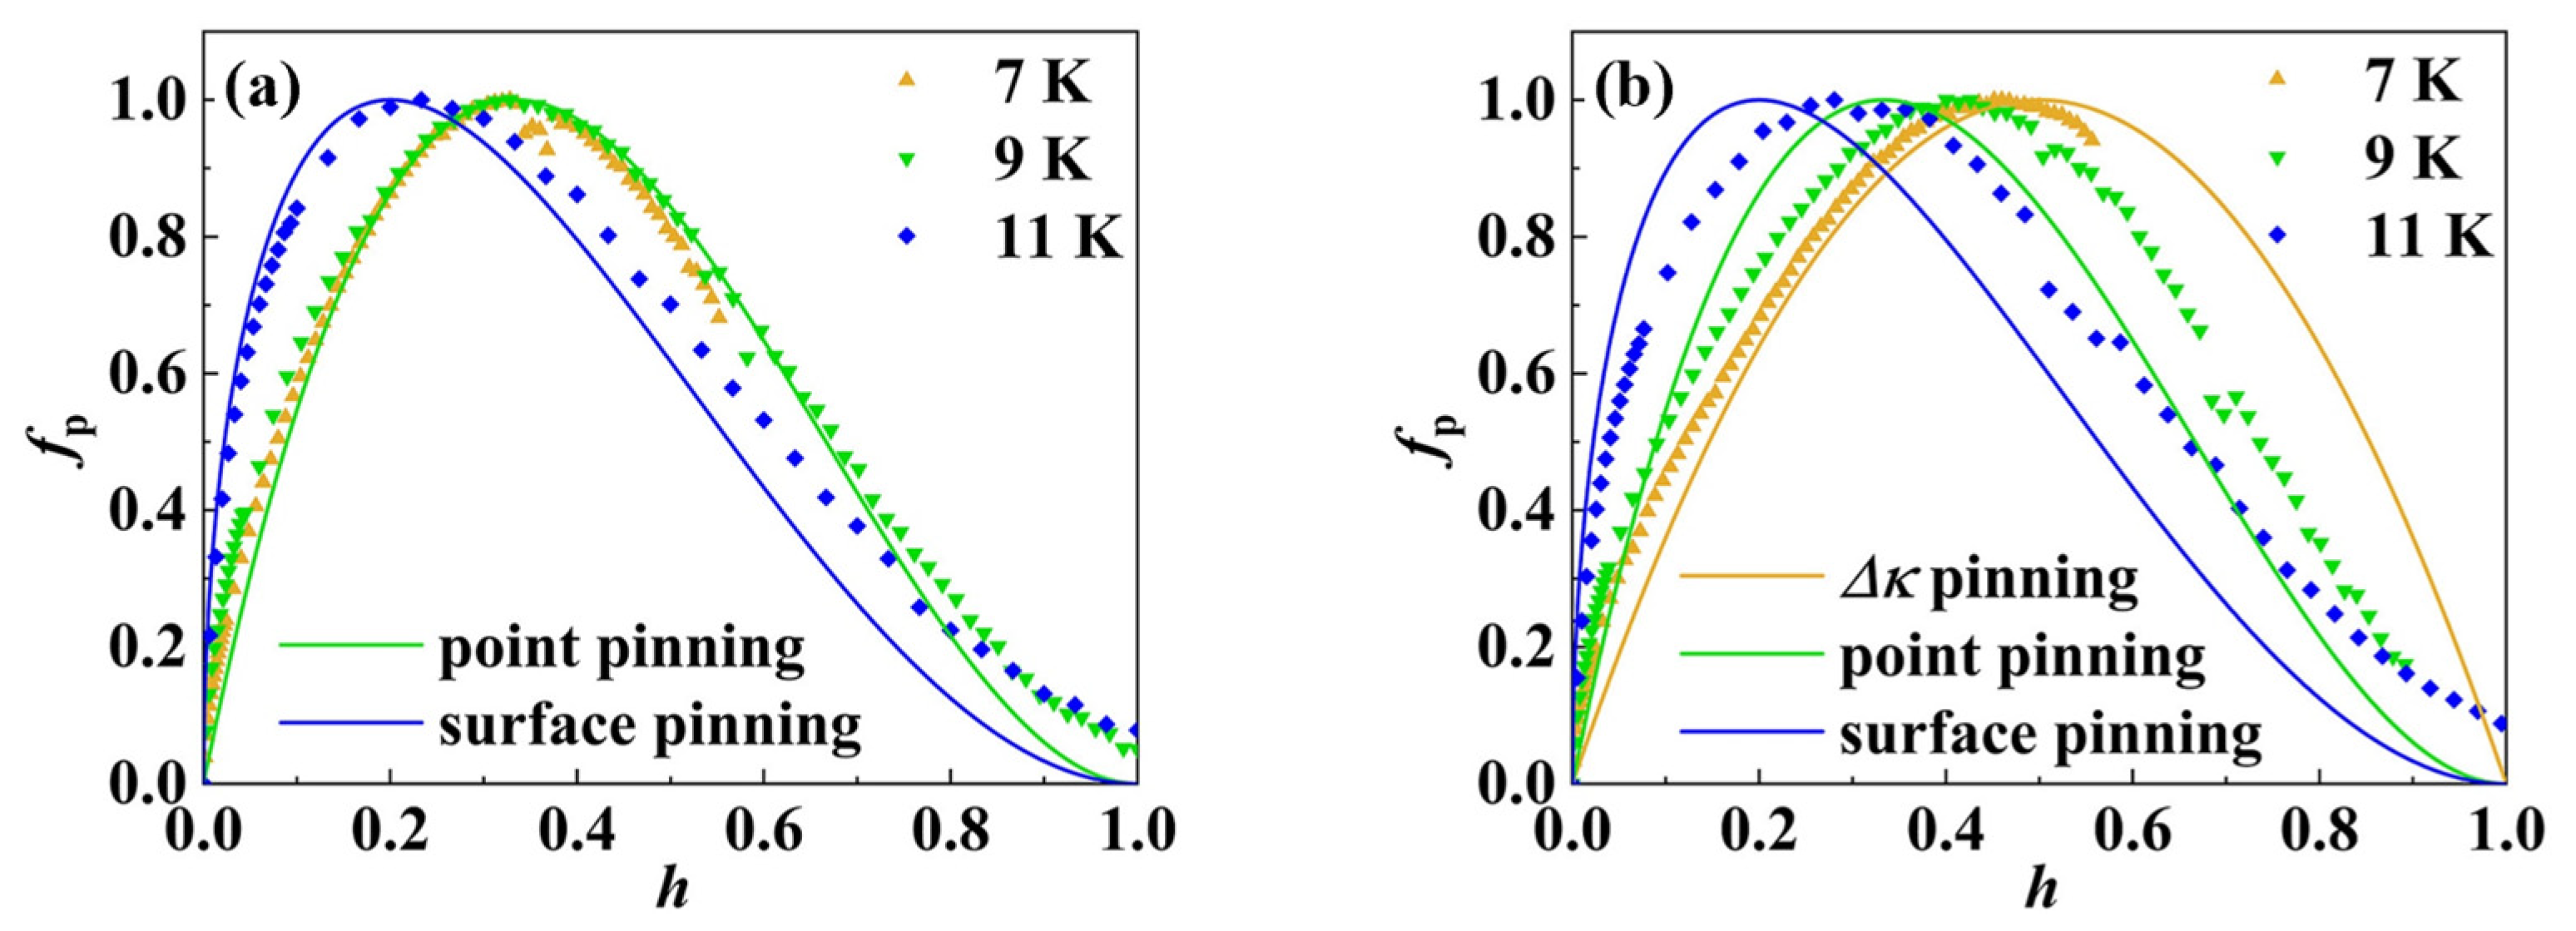
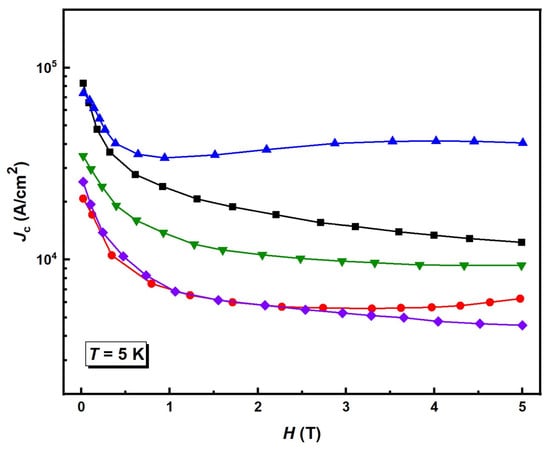
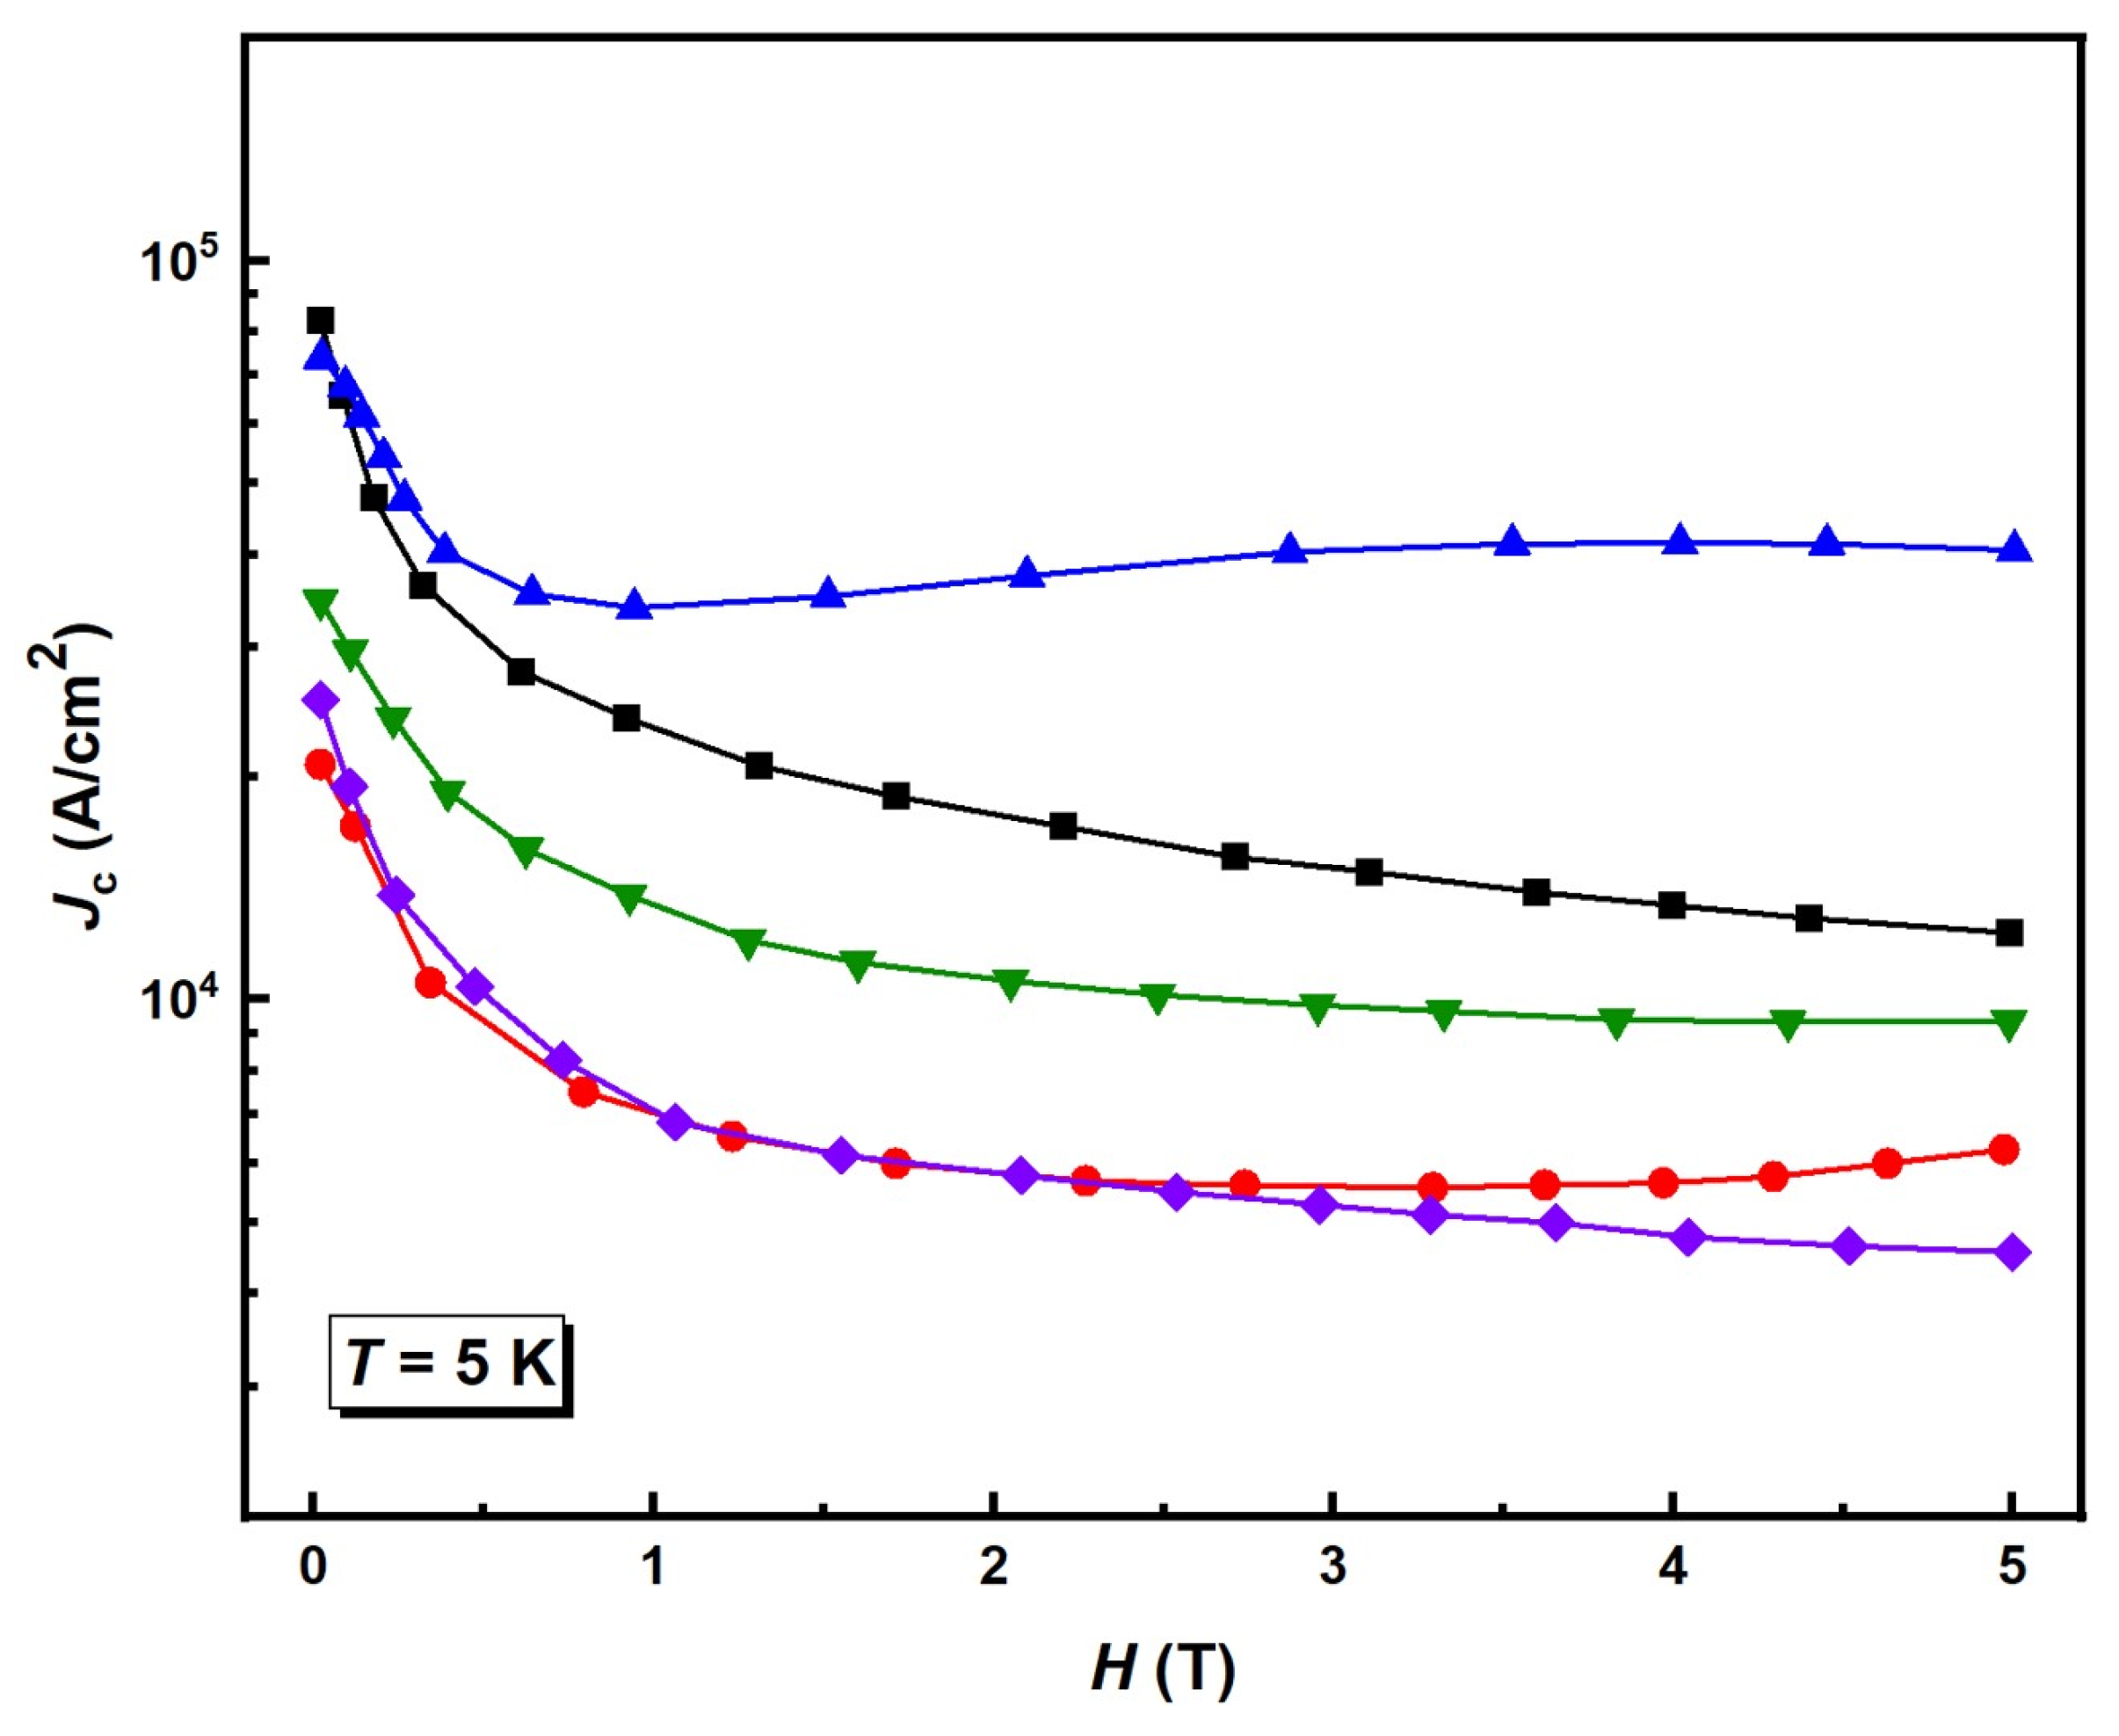
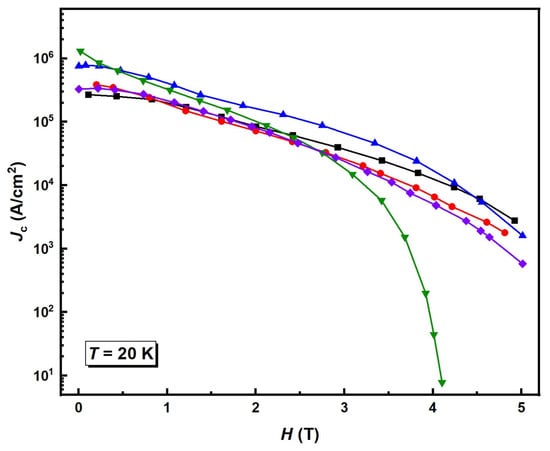
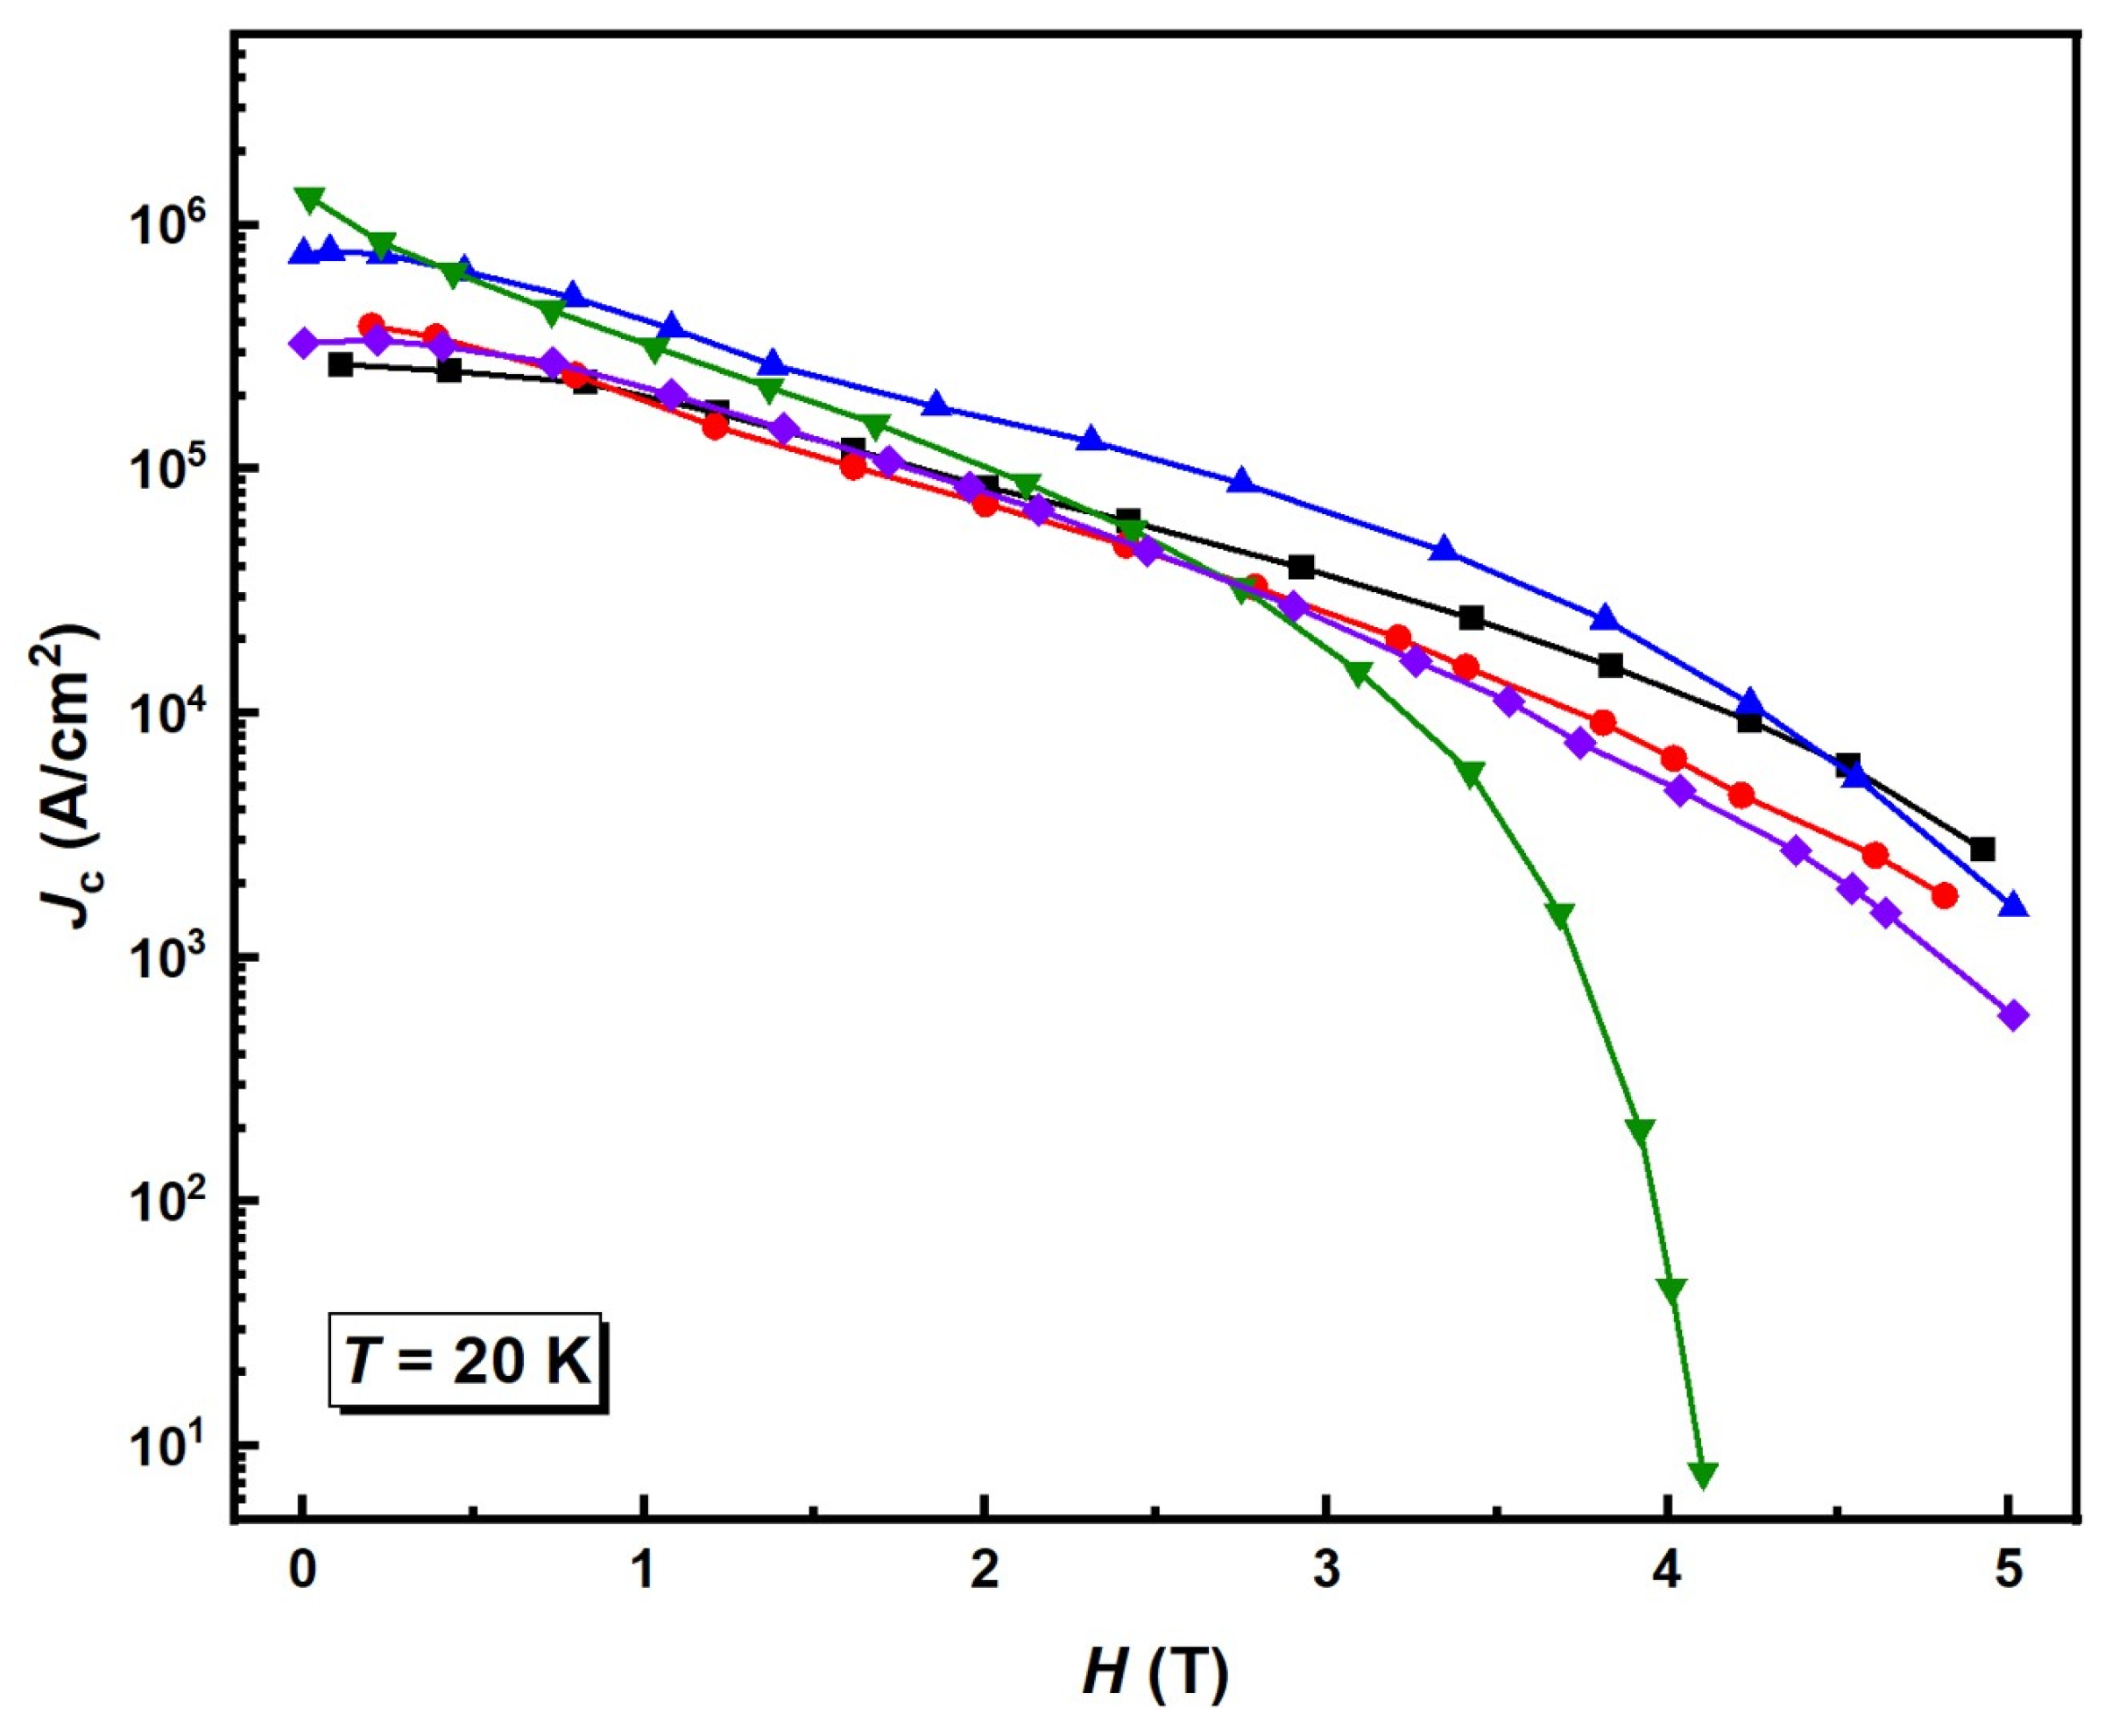
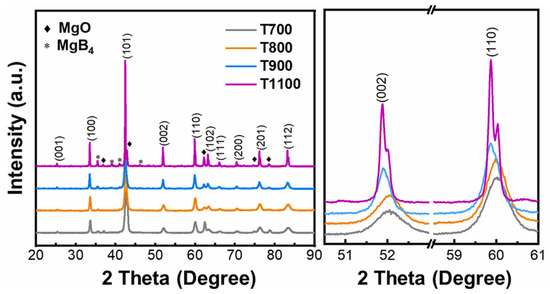
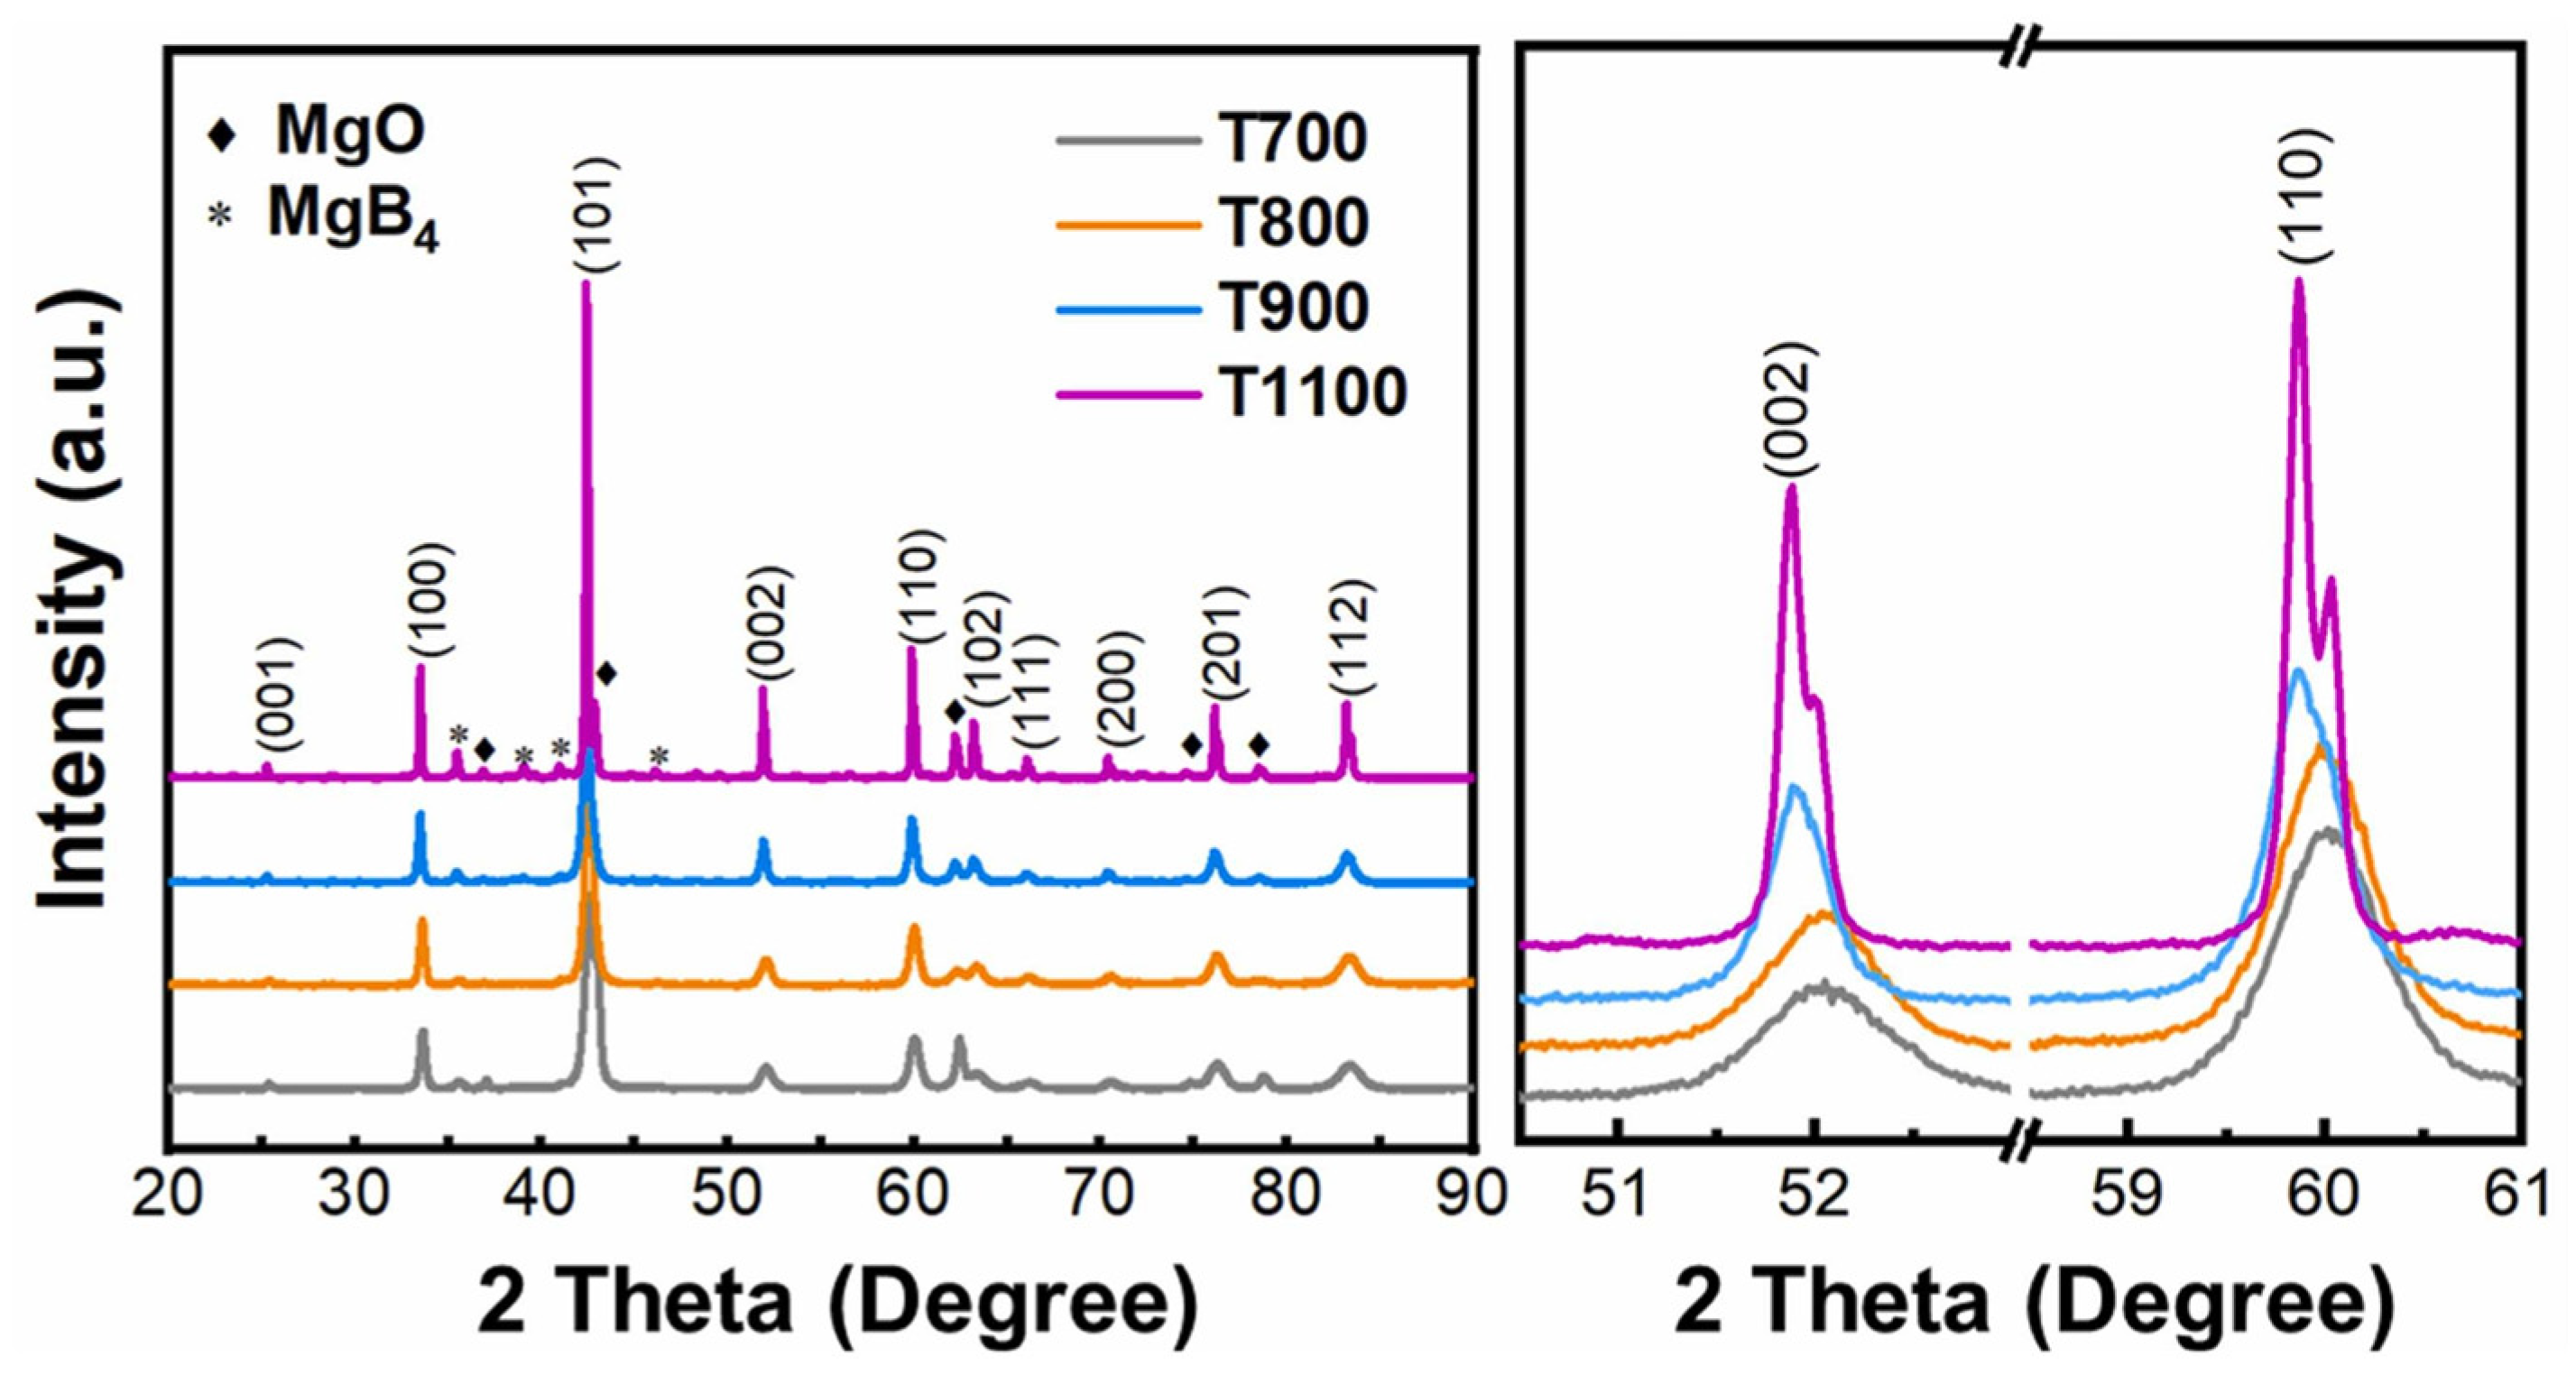
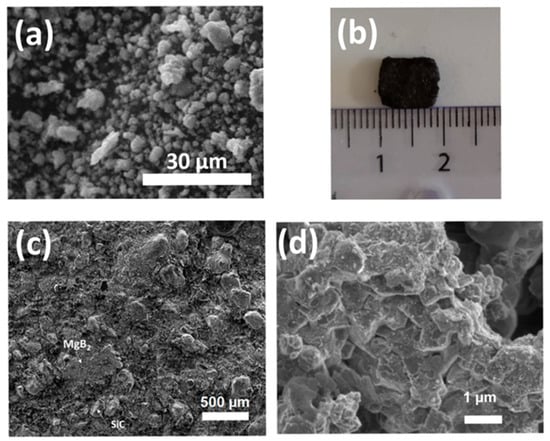
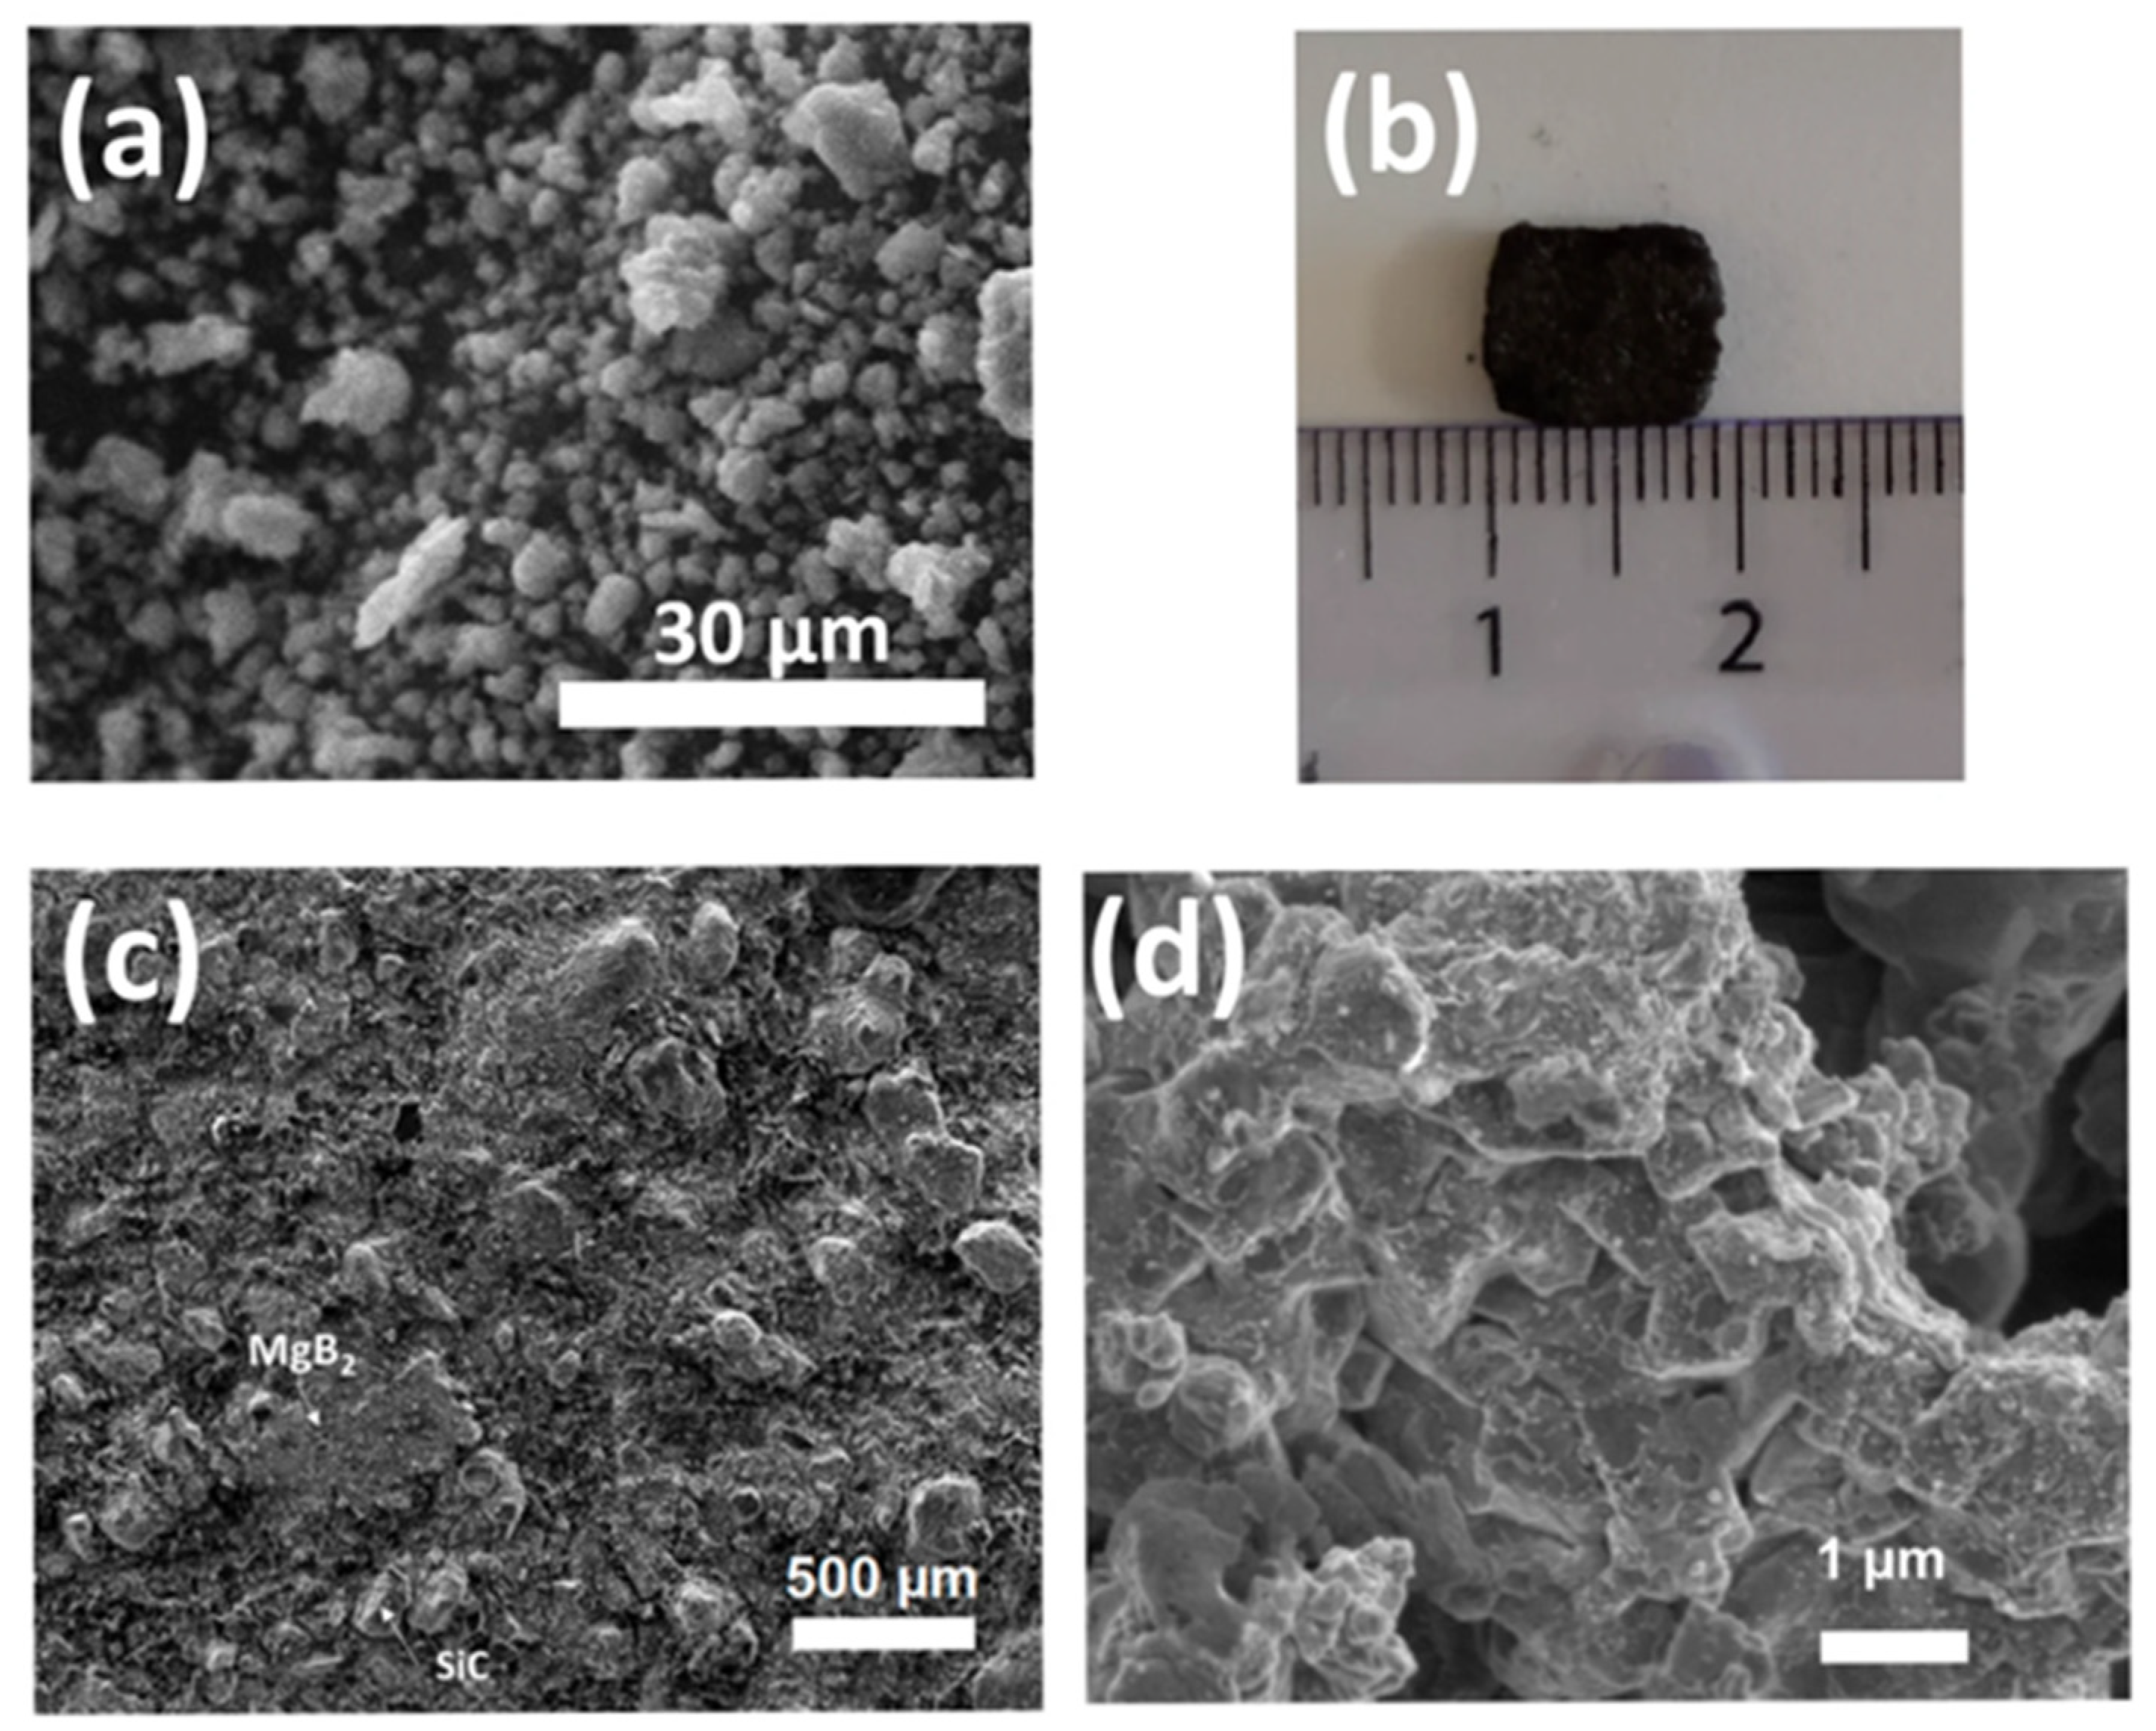
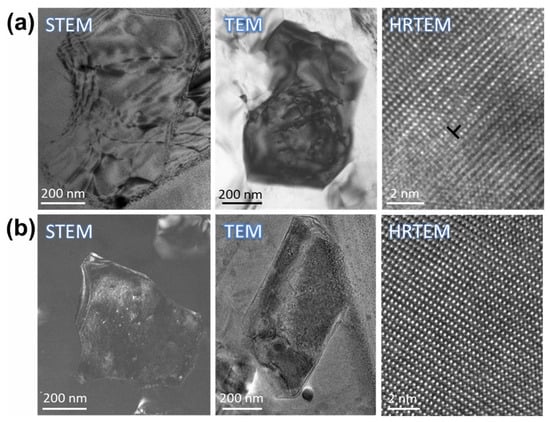
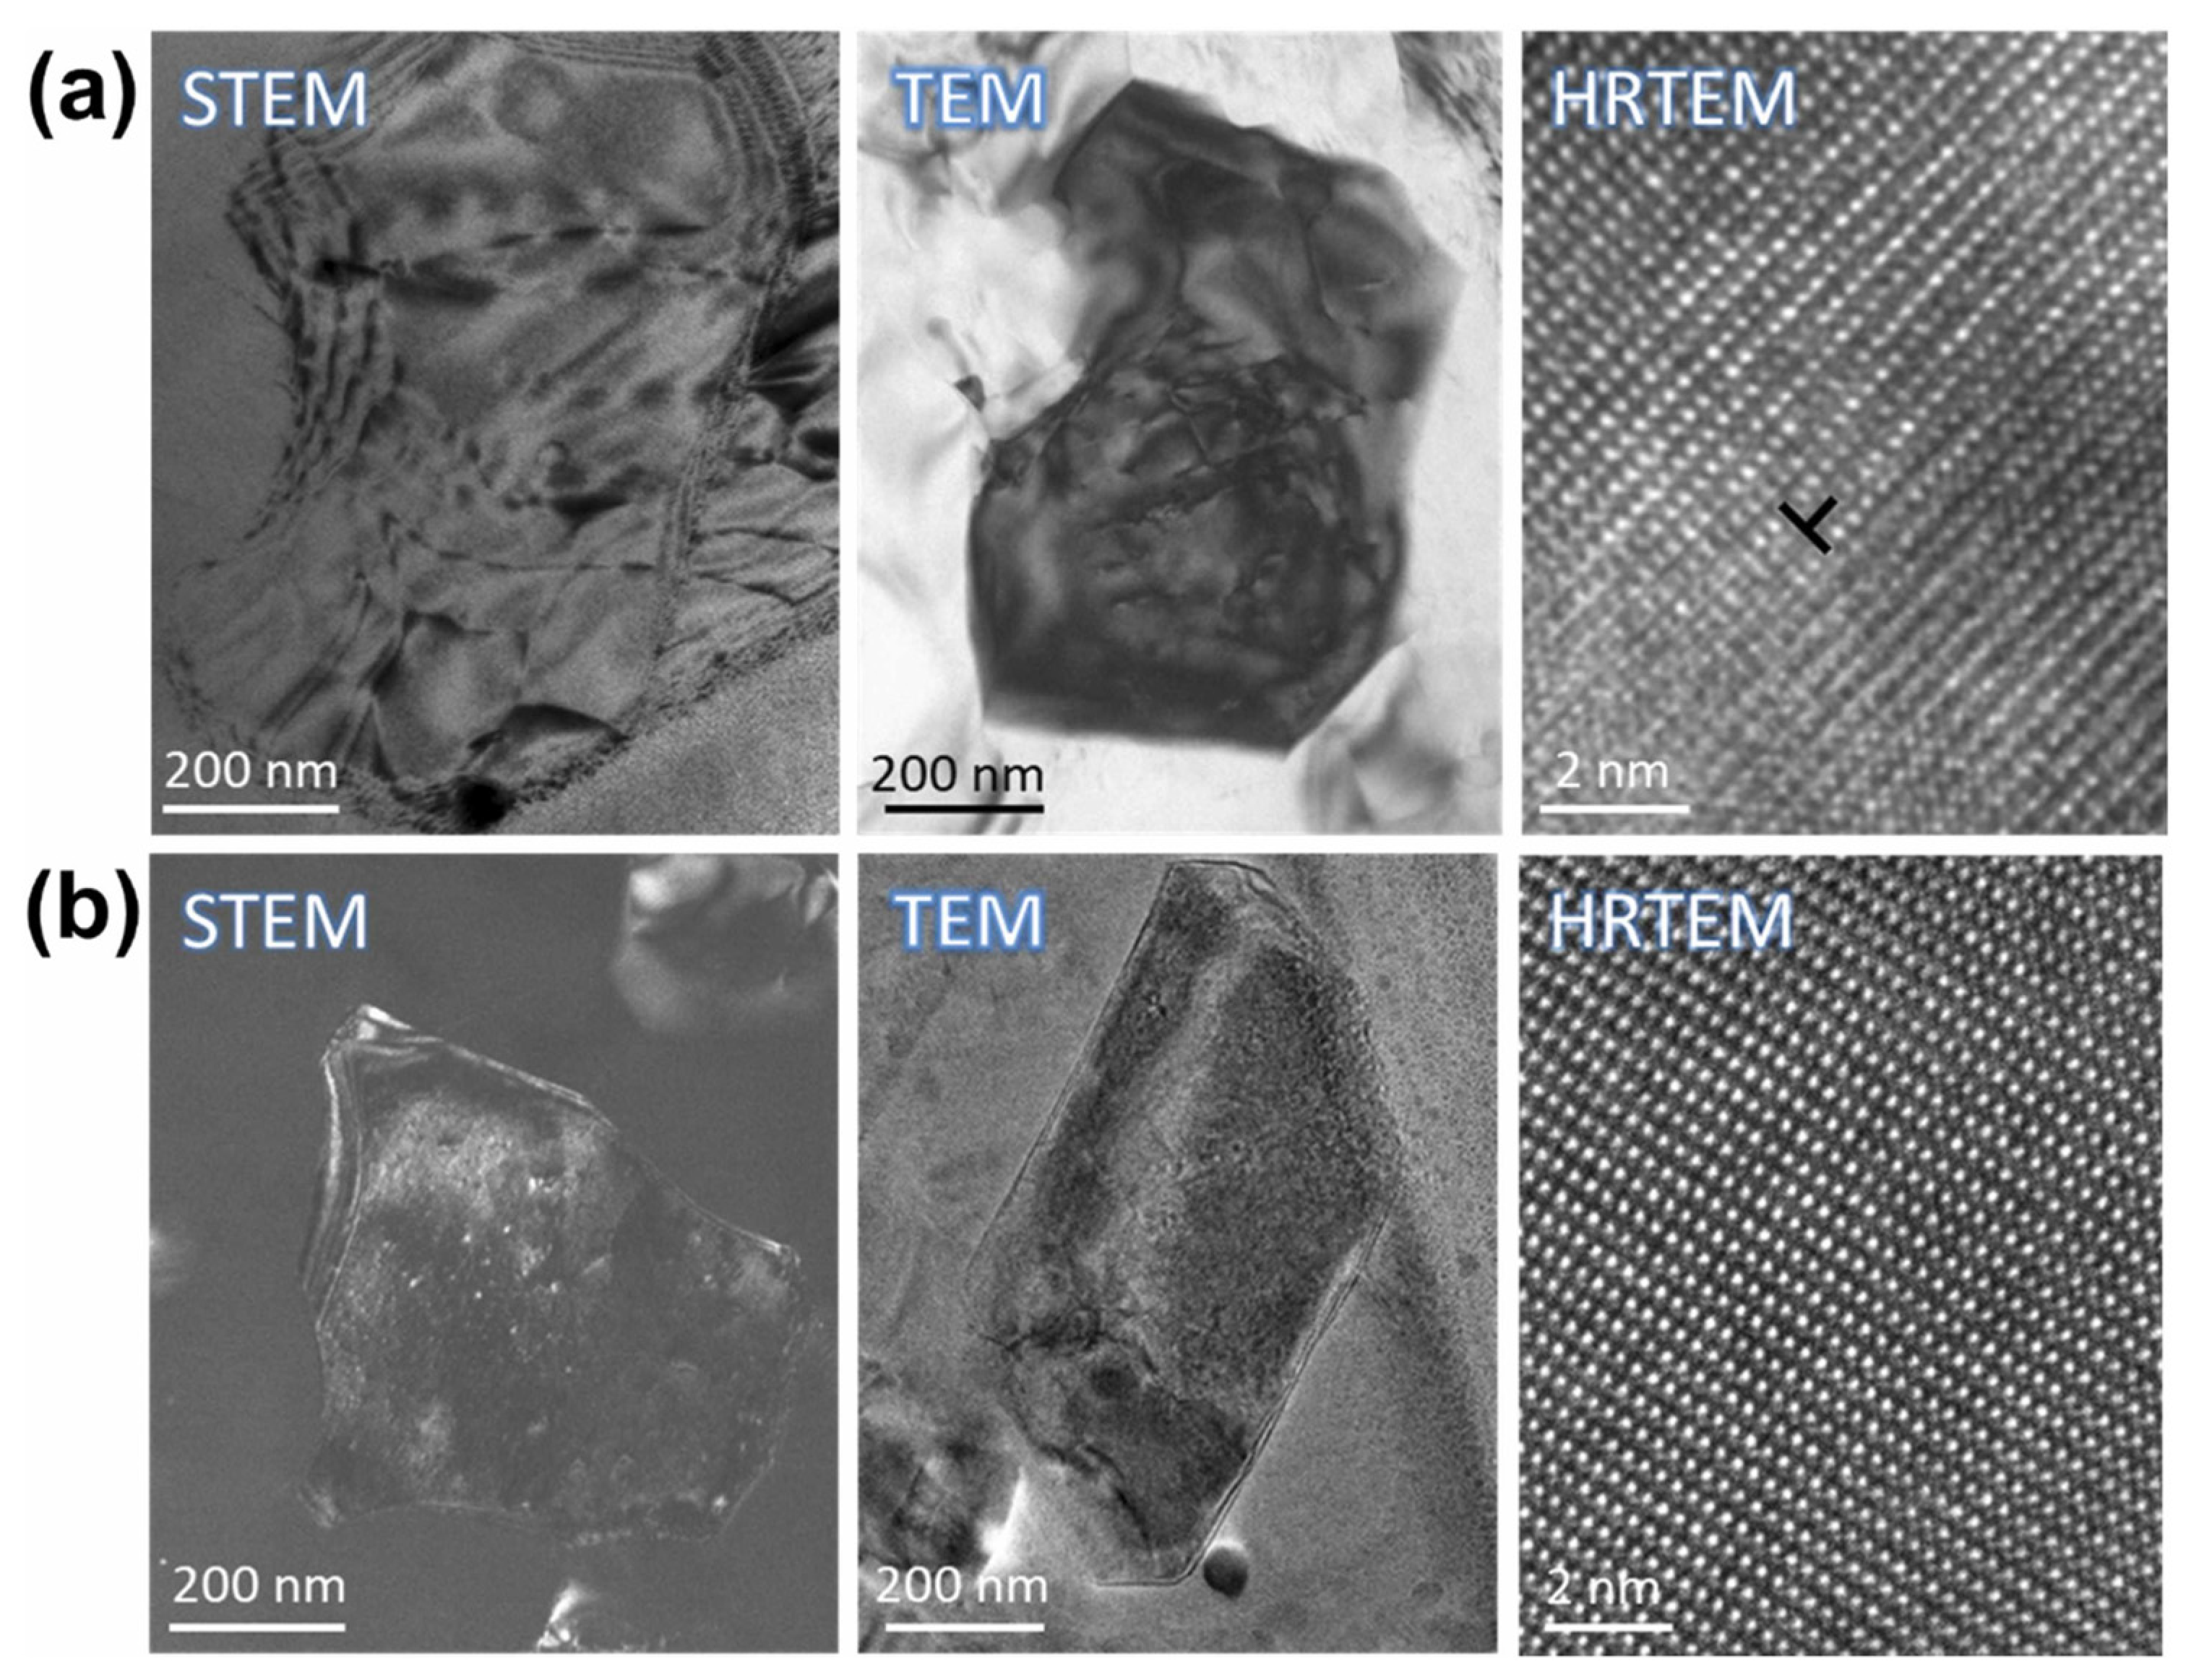
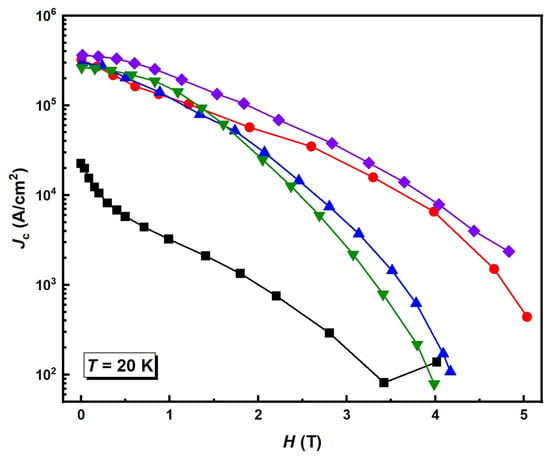
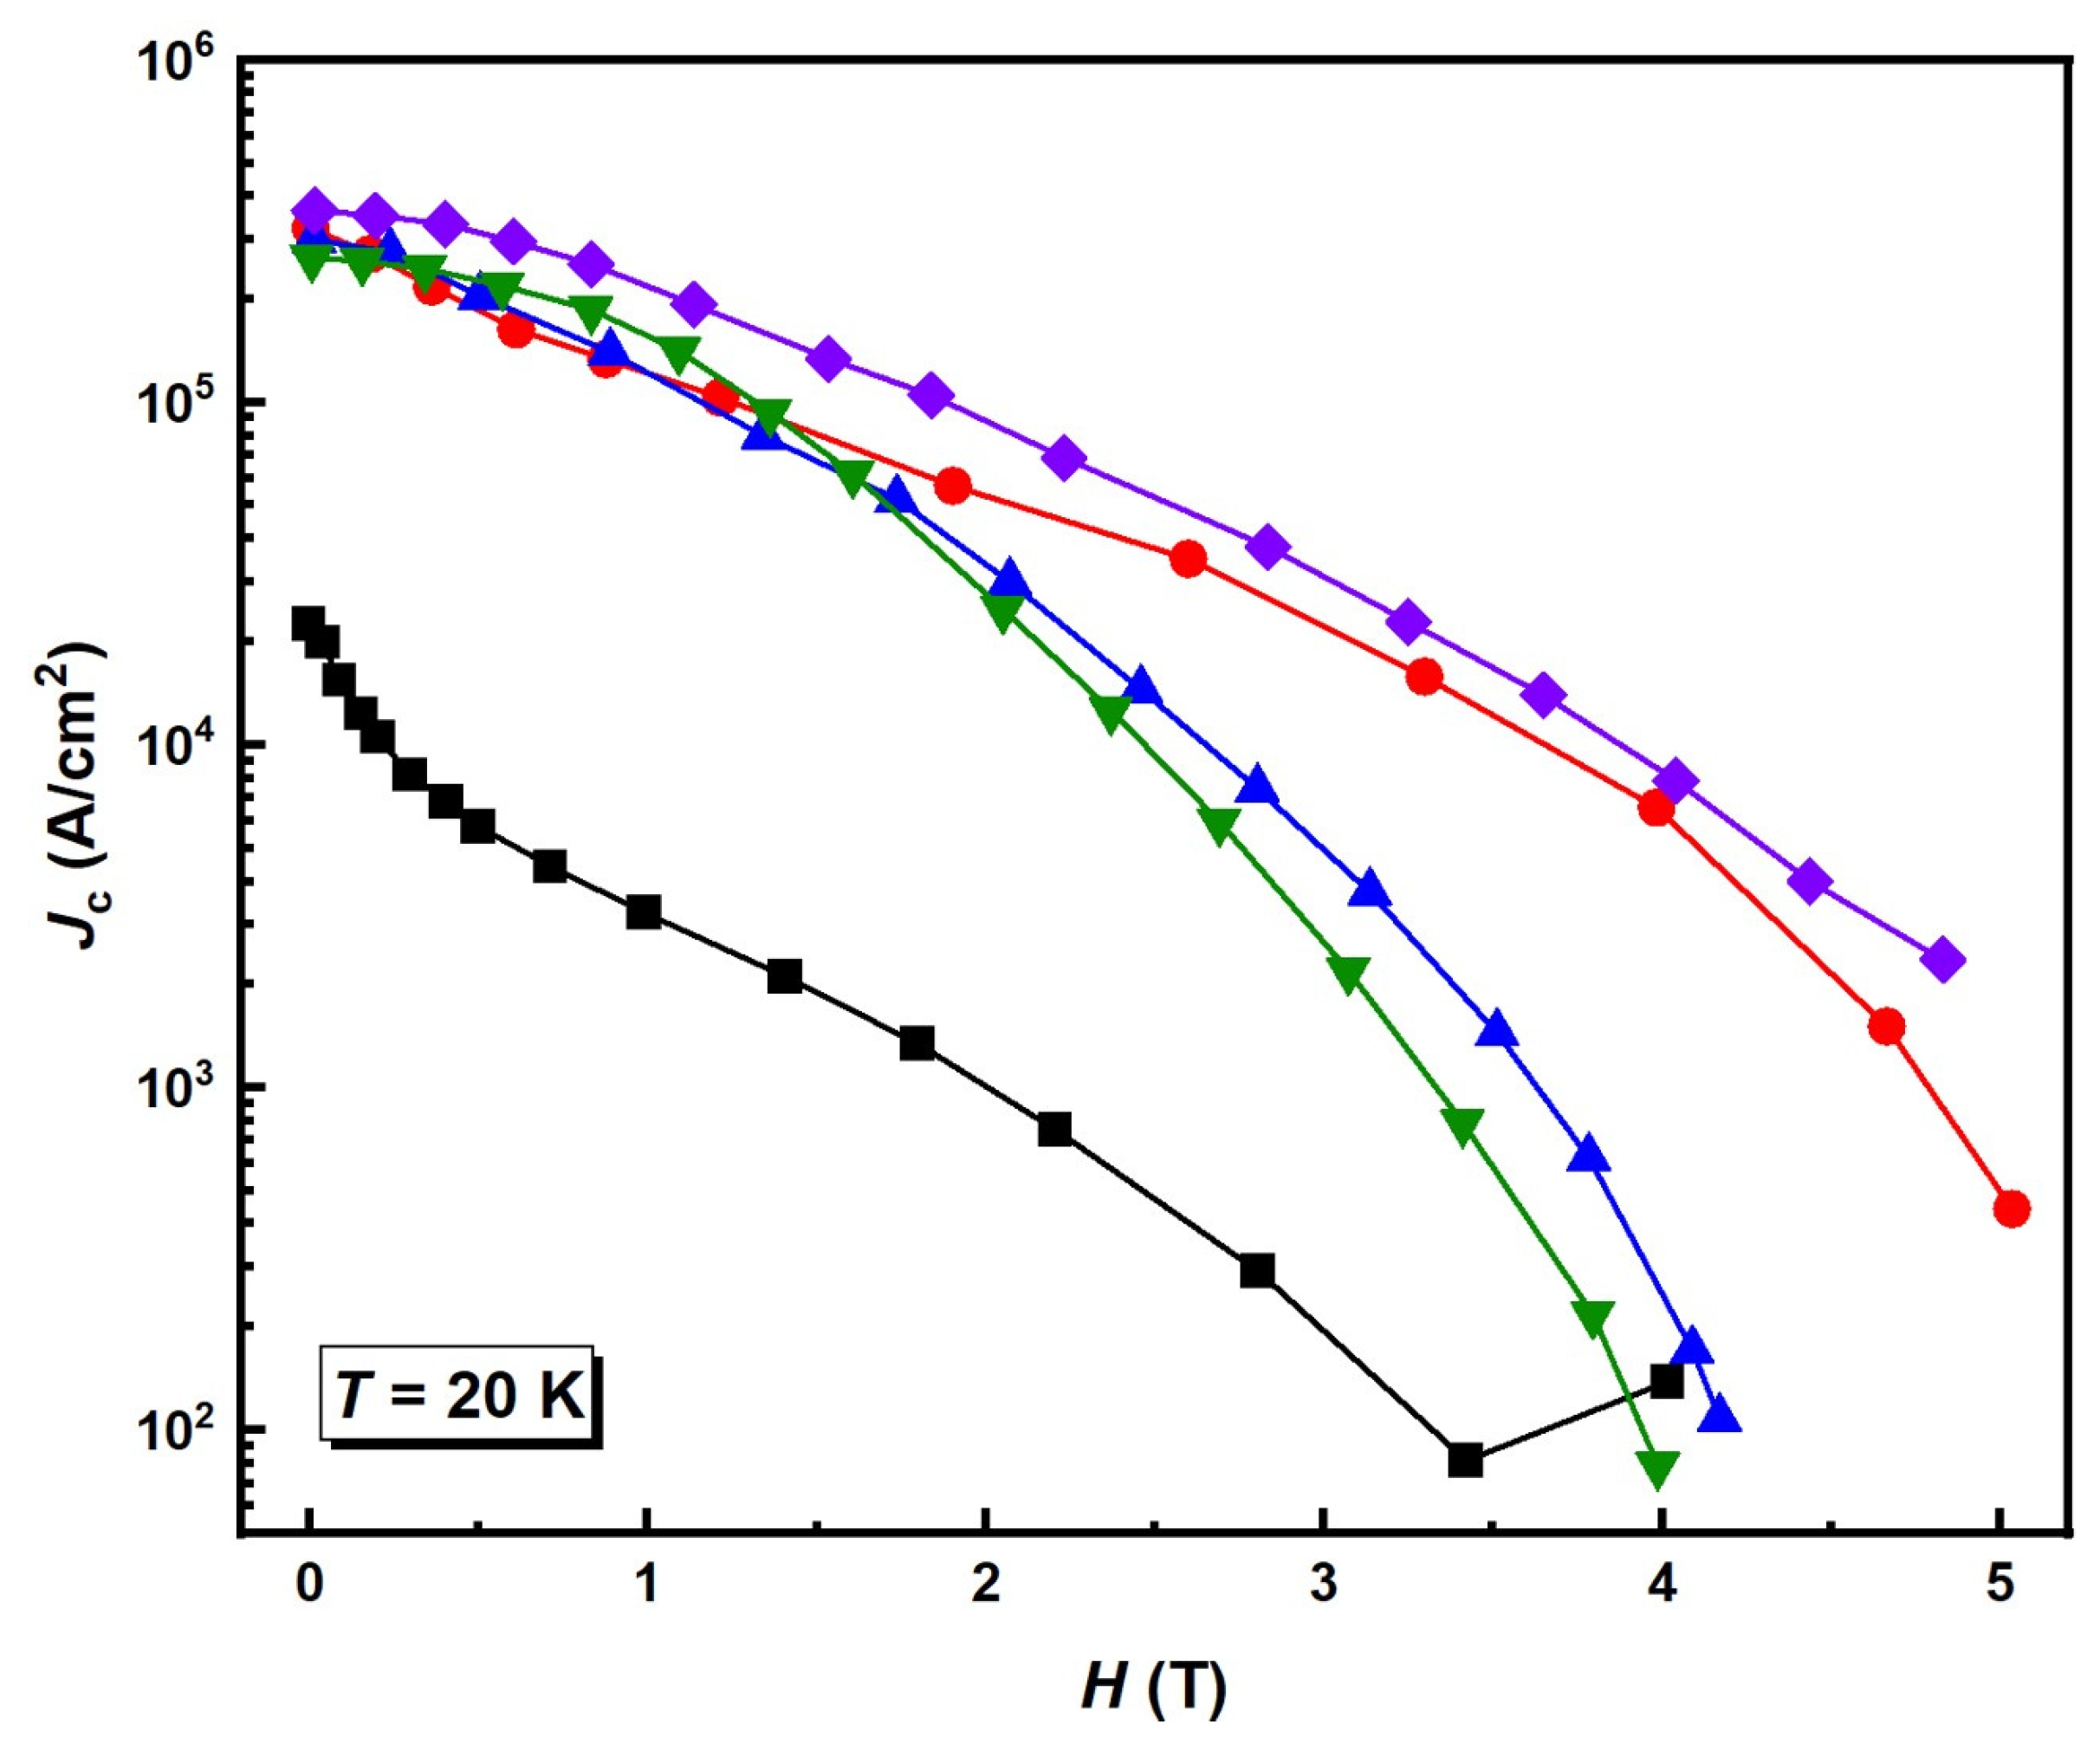

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.