Study of Molten Pool Evolution in VP-CMT Aluminium Alloy Arc Additive Manufacturing Under Different EP:EN Ratios

Abstract
1. Introduction
2. Experimental Equipment, Materials and Research Methods
2.1. Experimental Materials
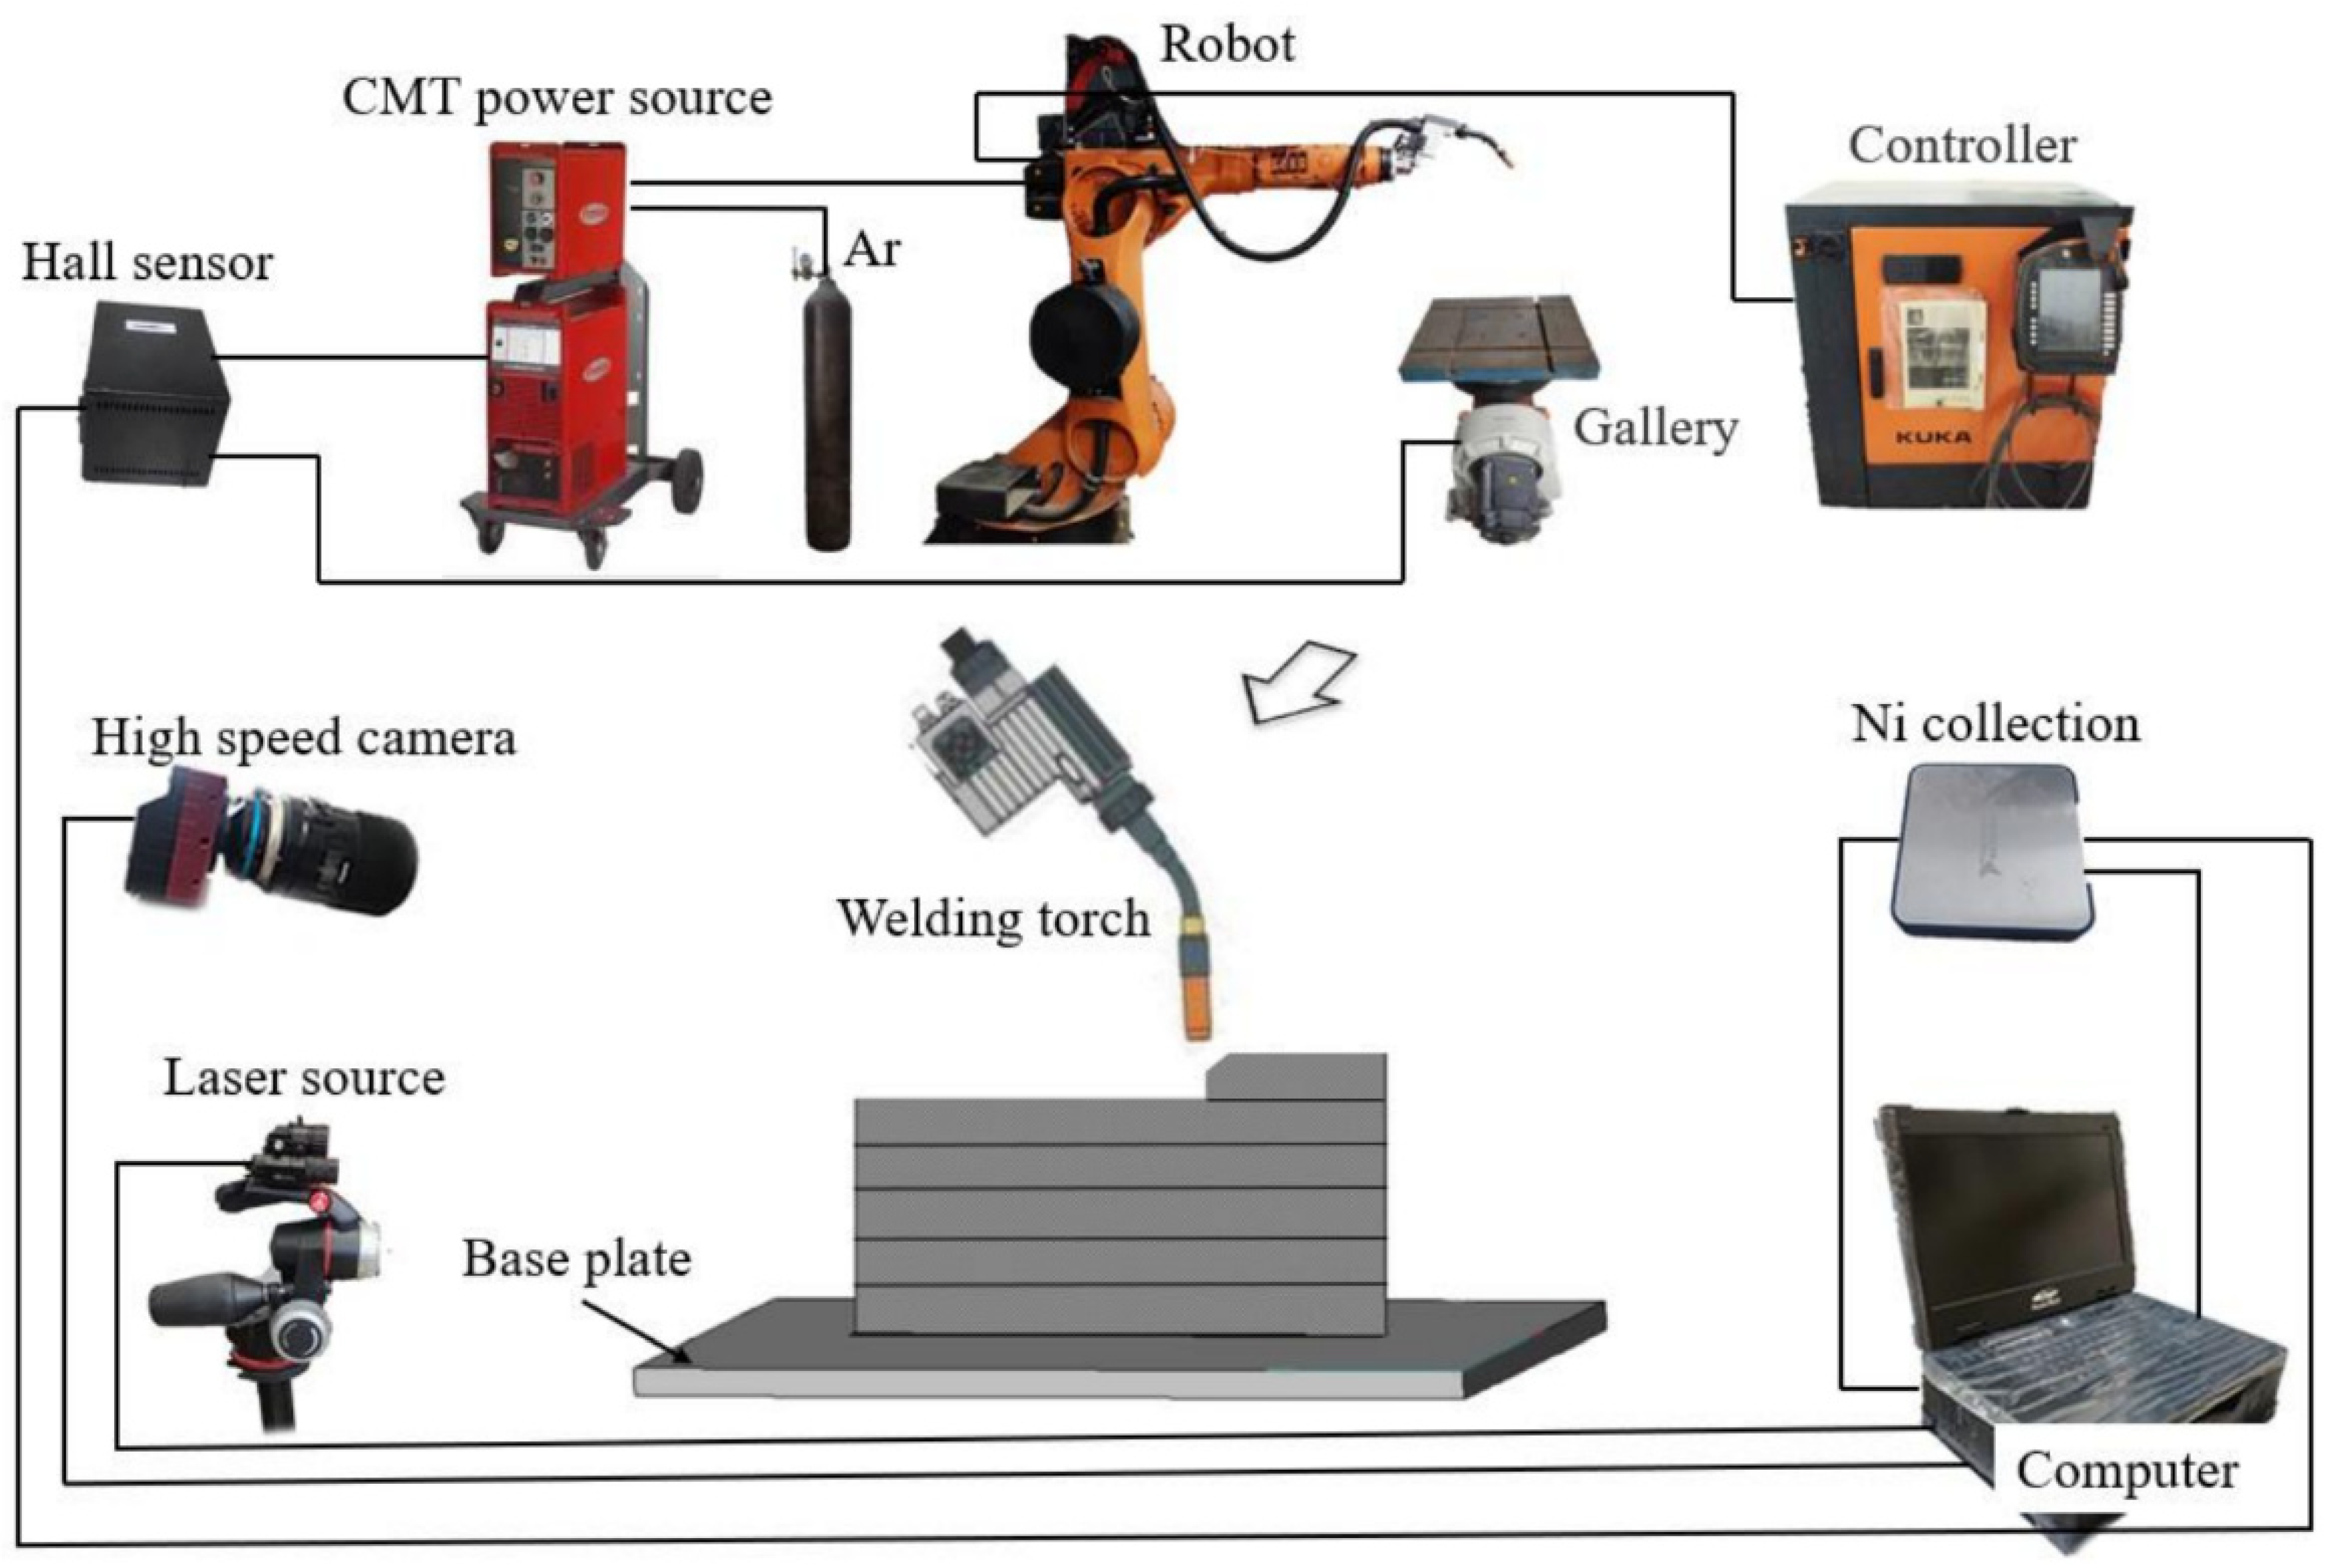
2.2. Arc Additive Manufacturing System and High-Speed Camera System
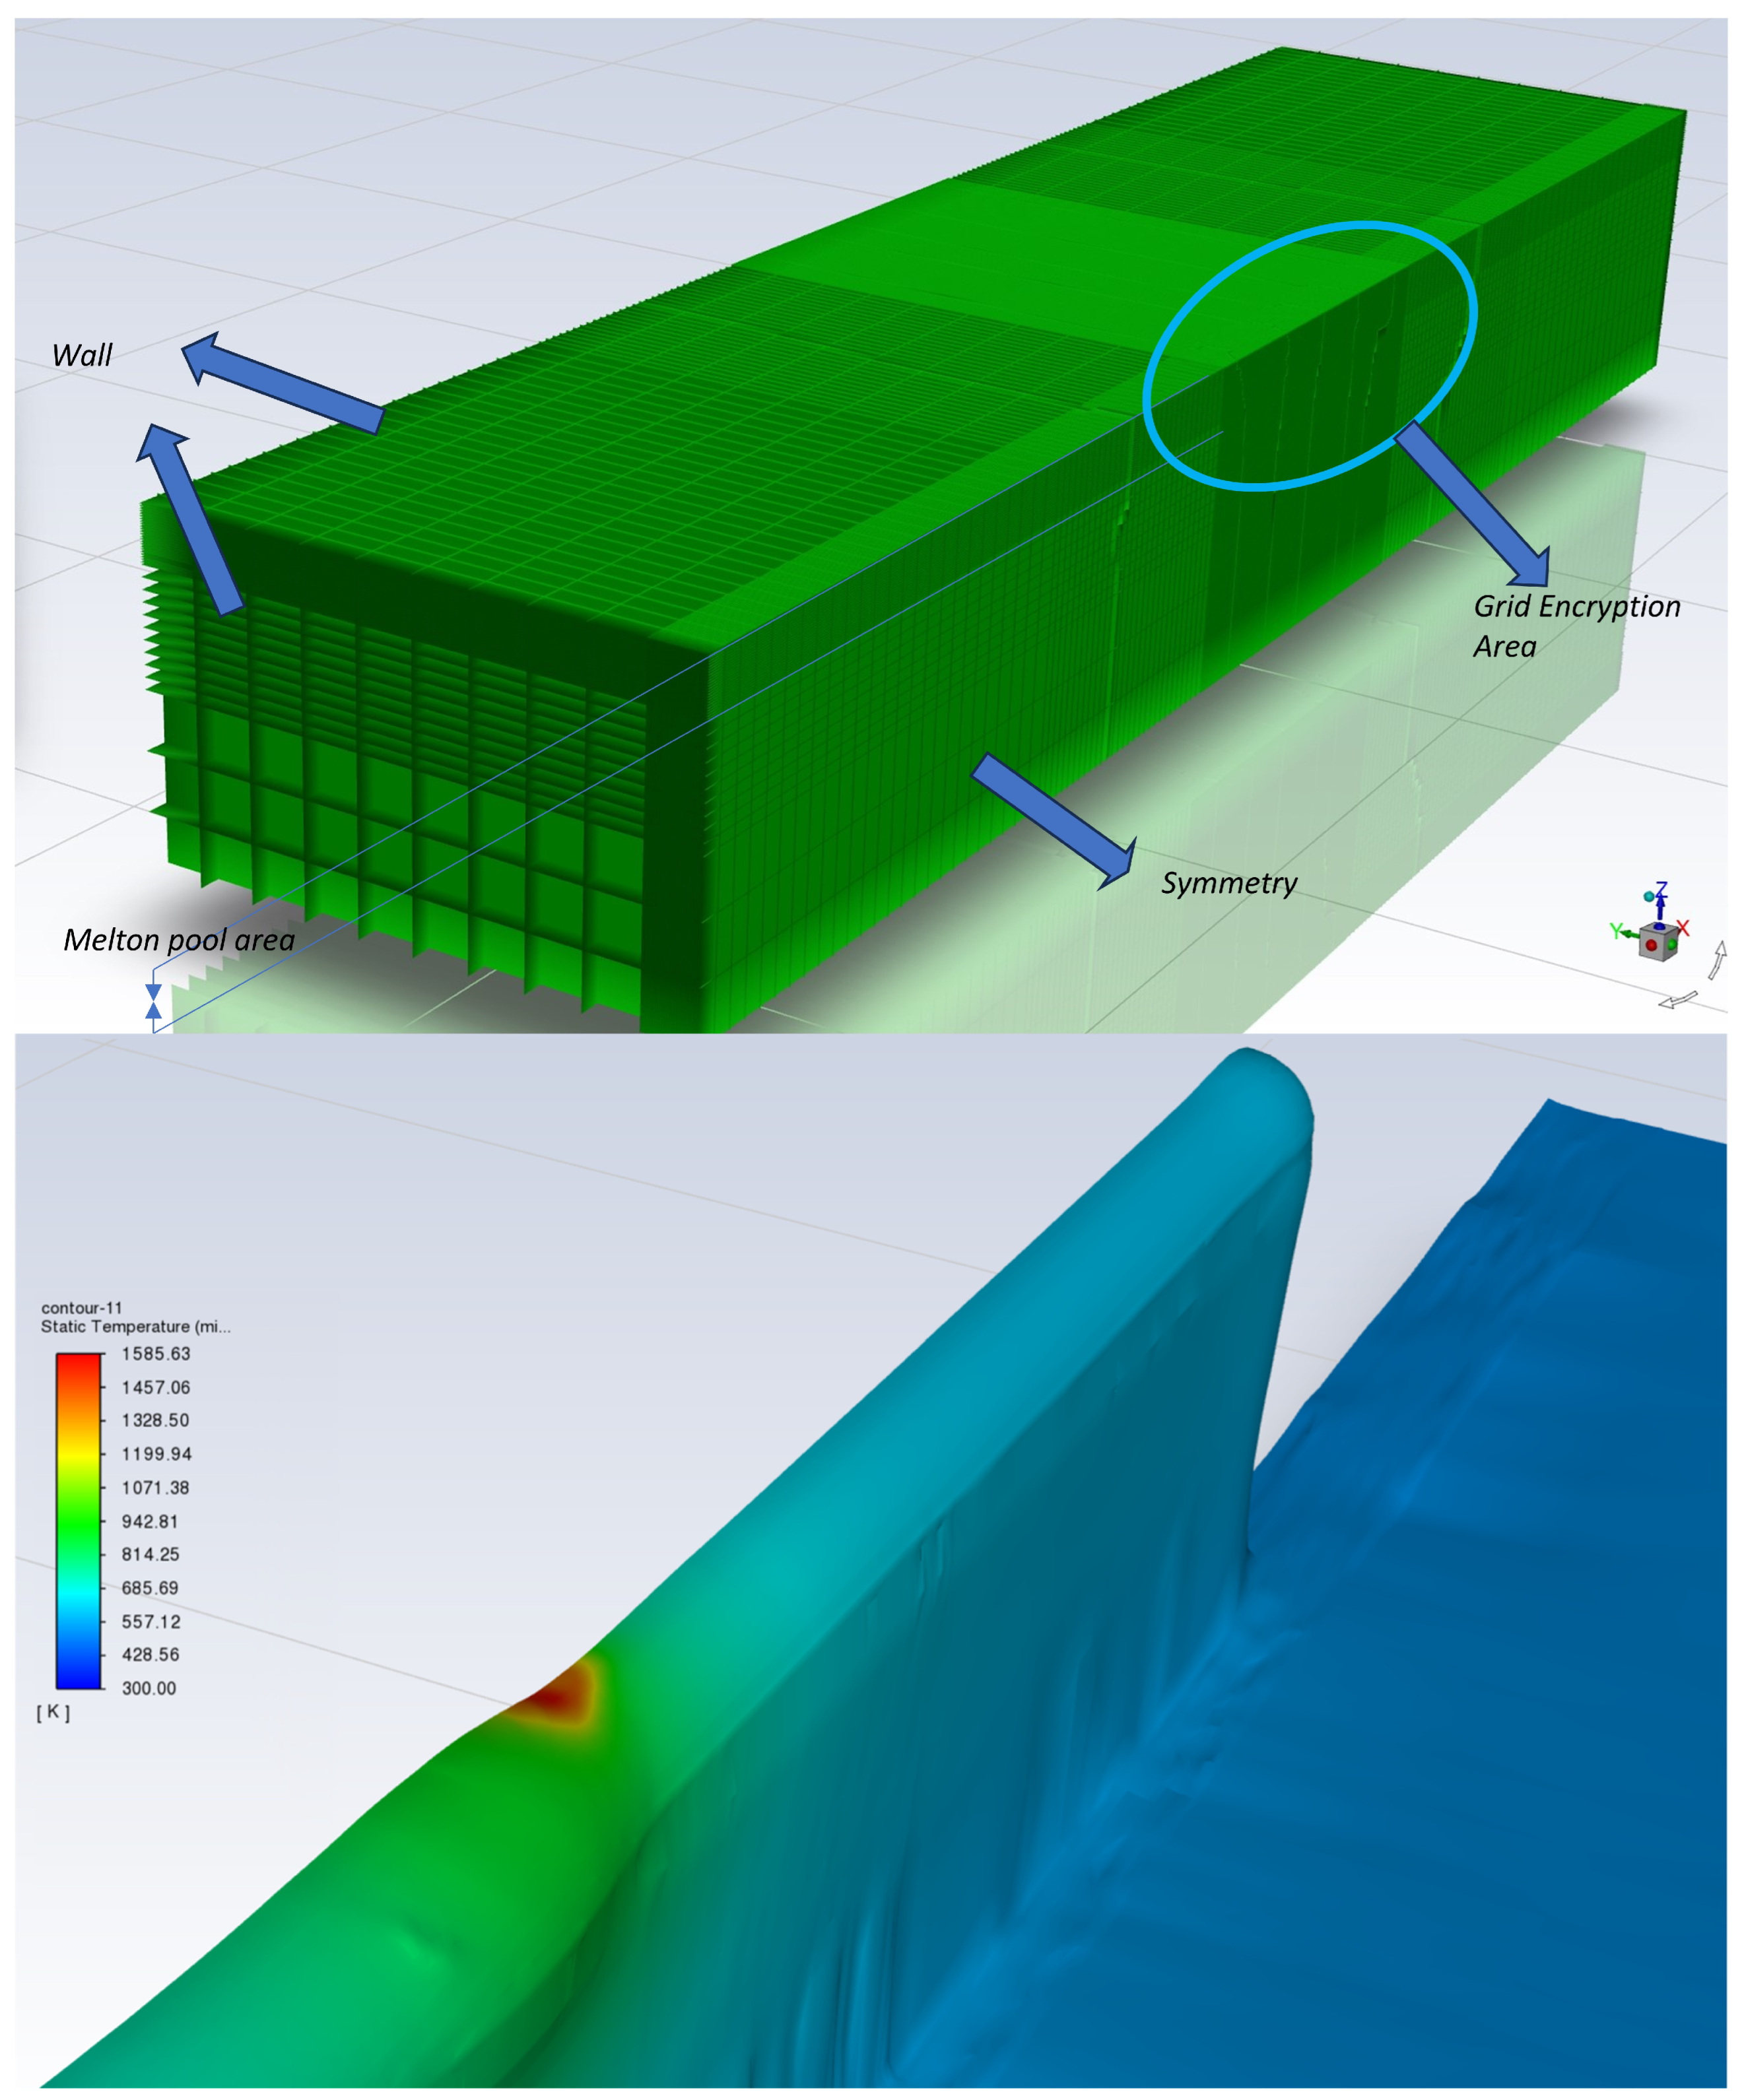
3. Establishing a Multi-Layer Single-Pass Cladding Droplet Melt Pool Model
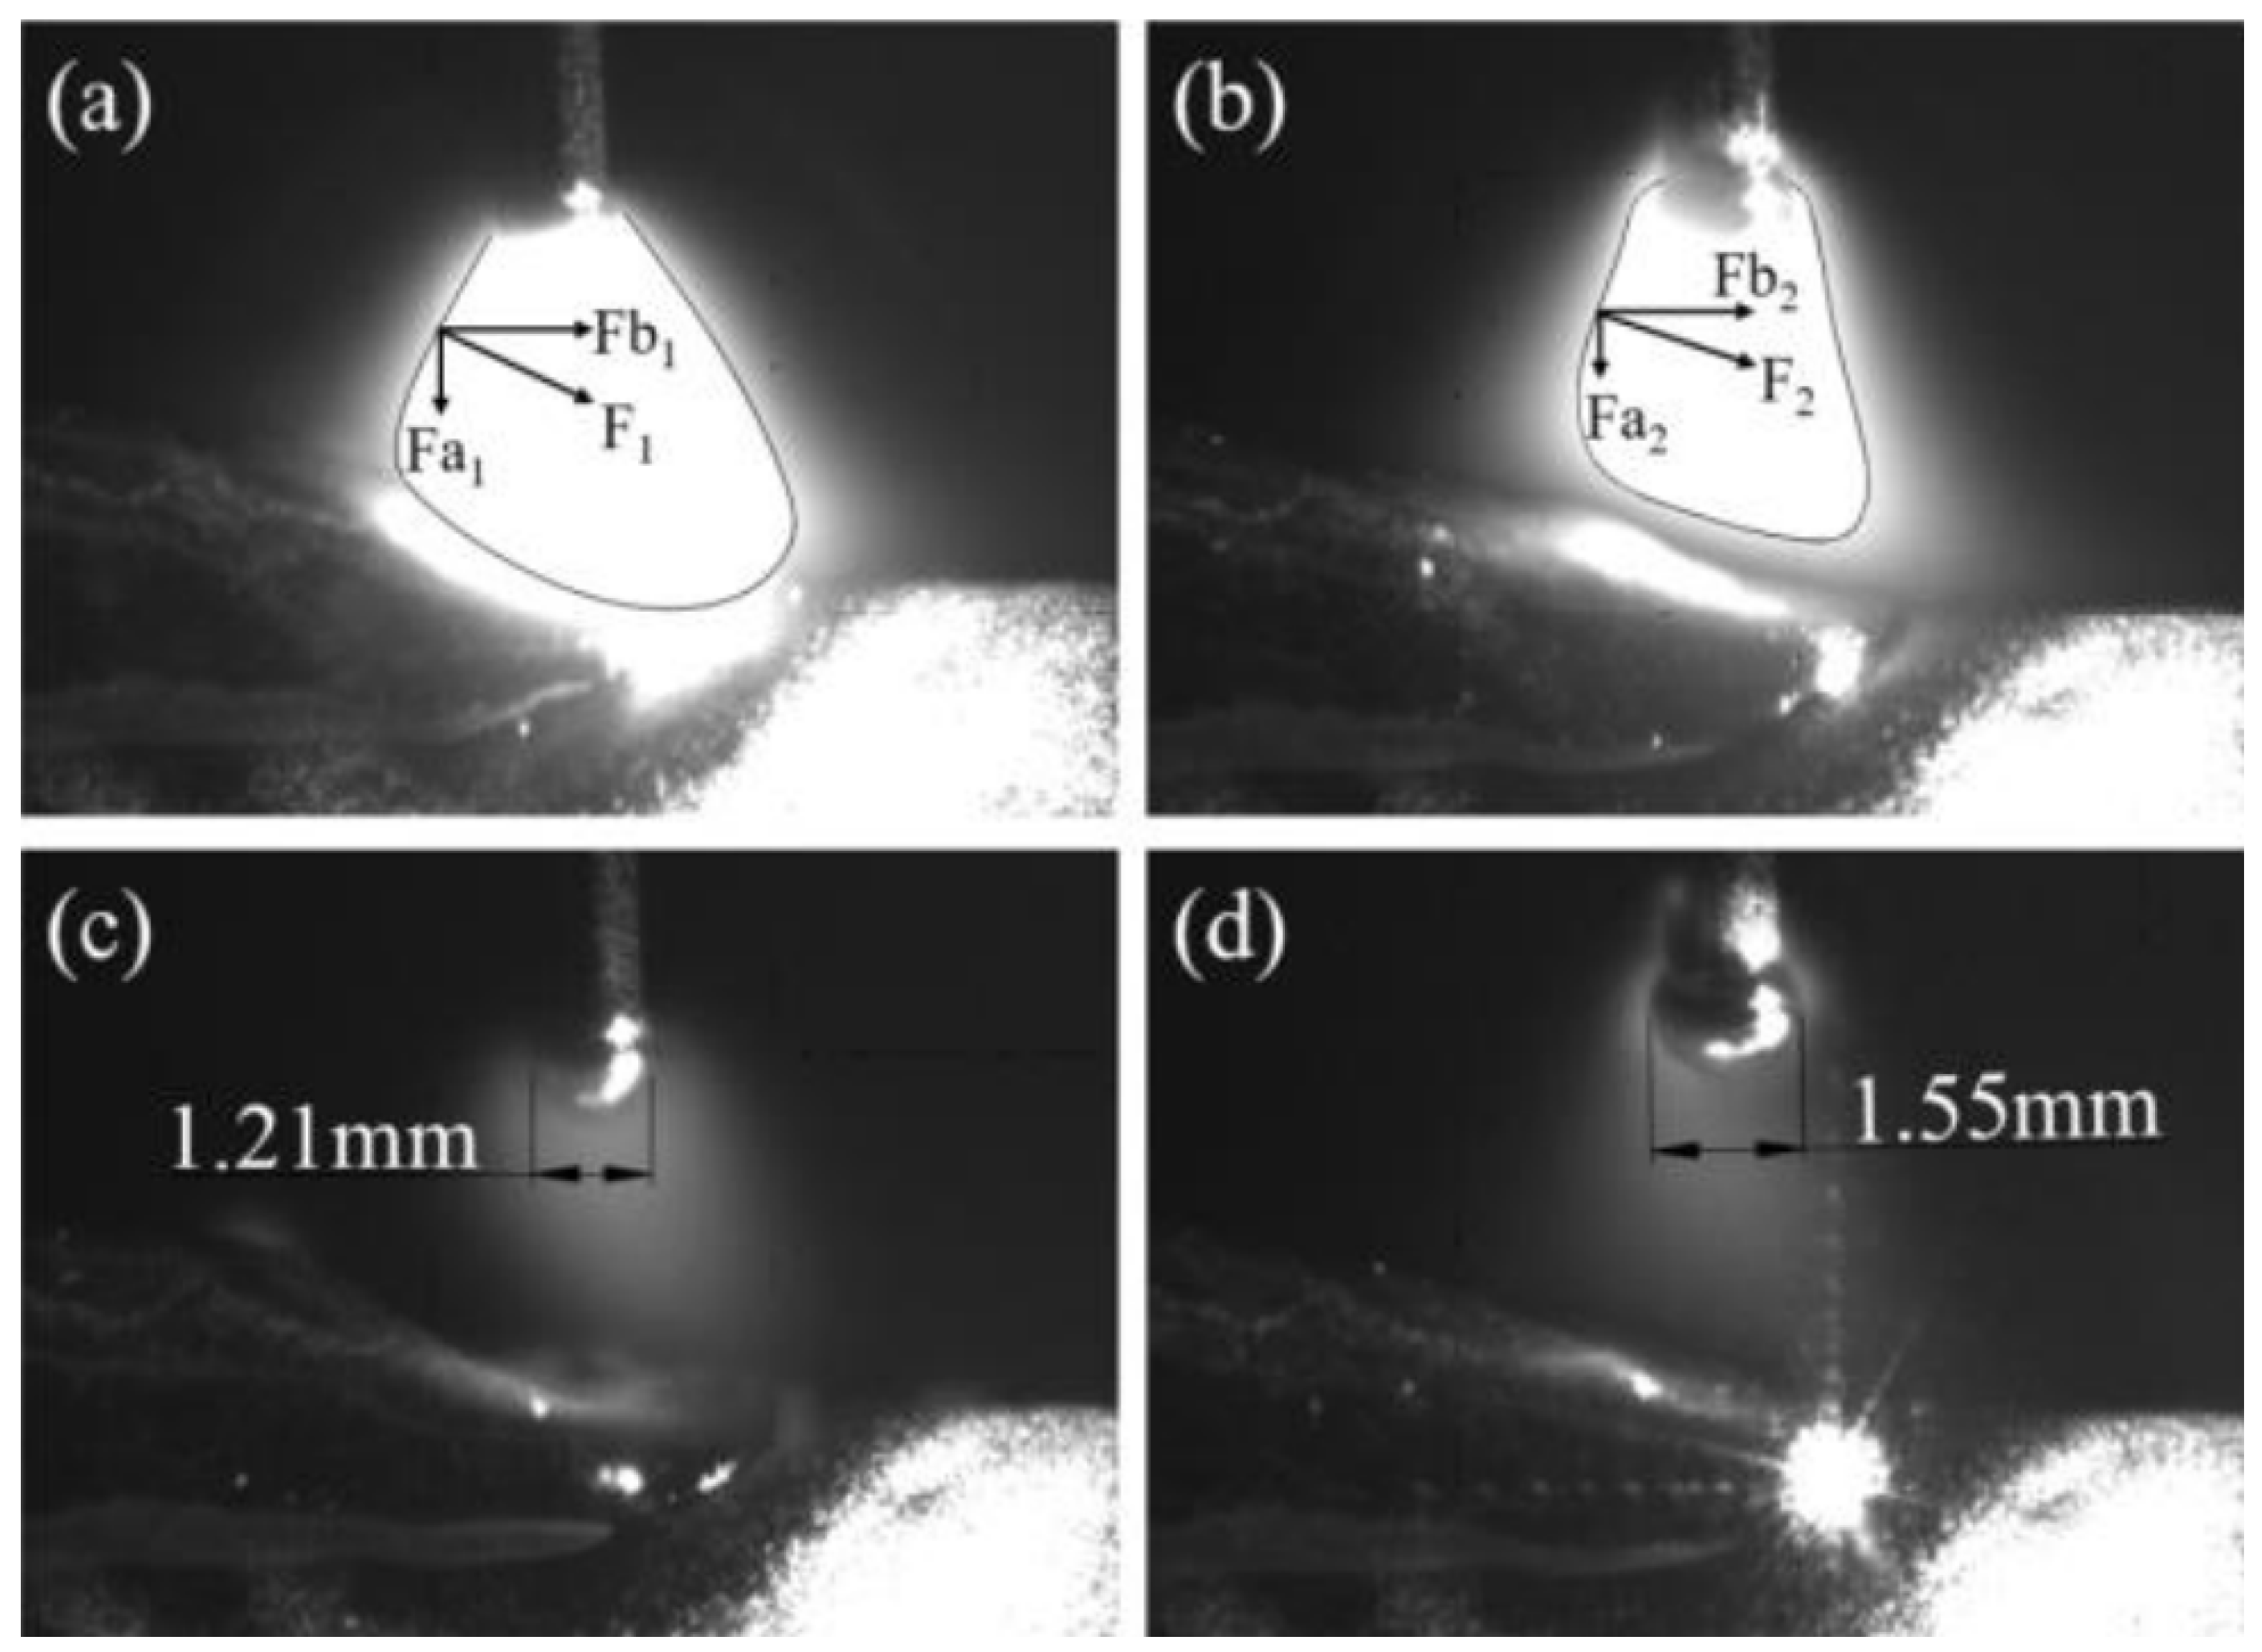
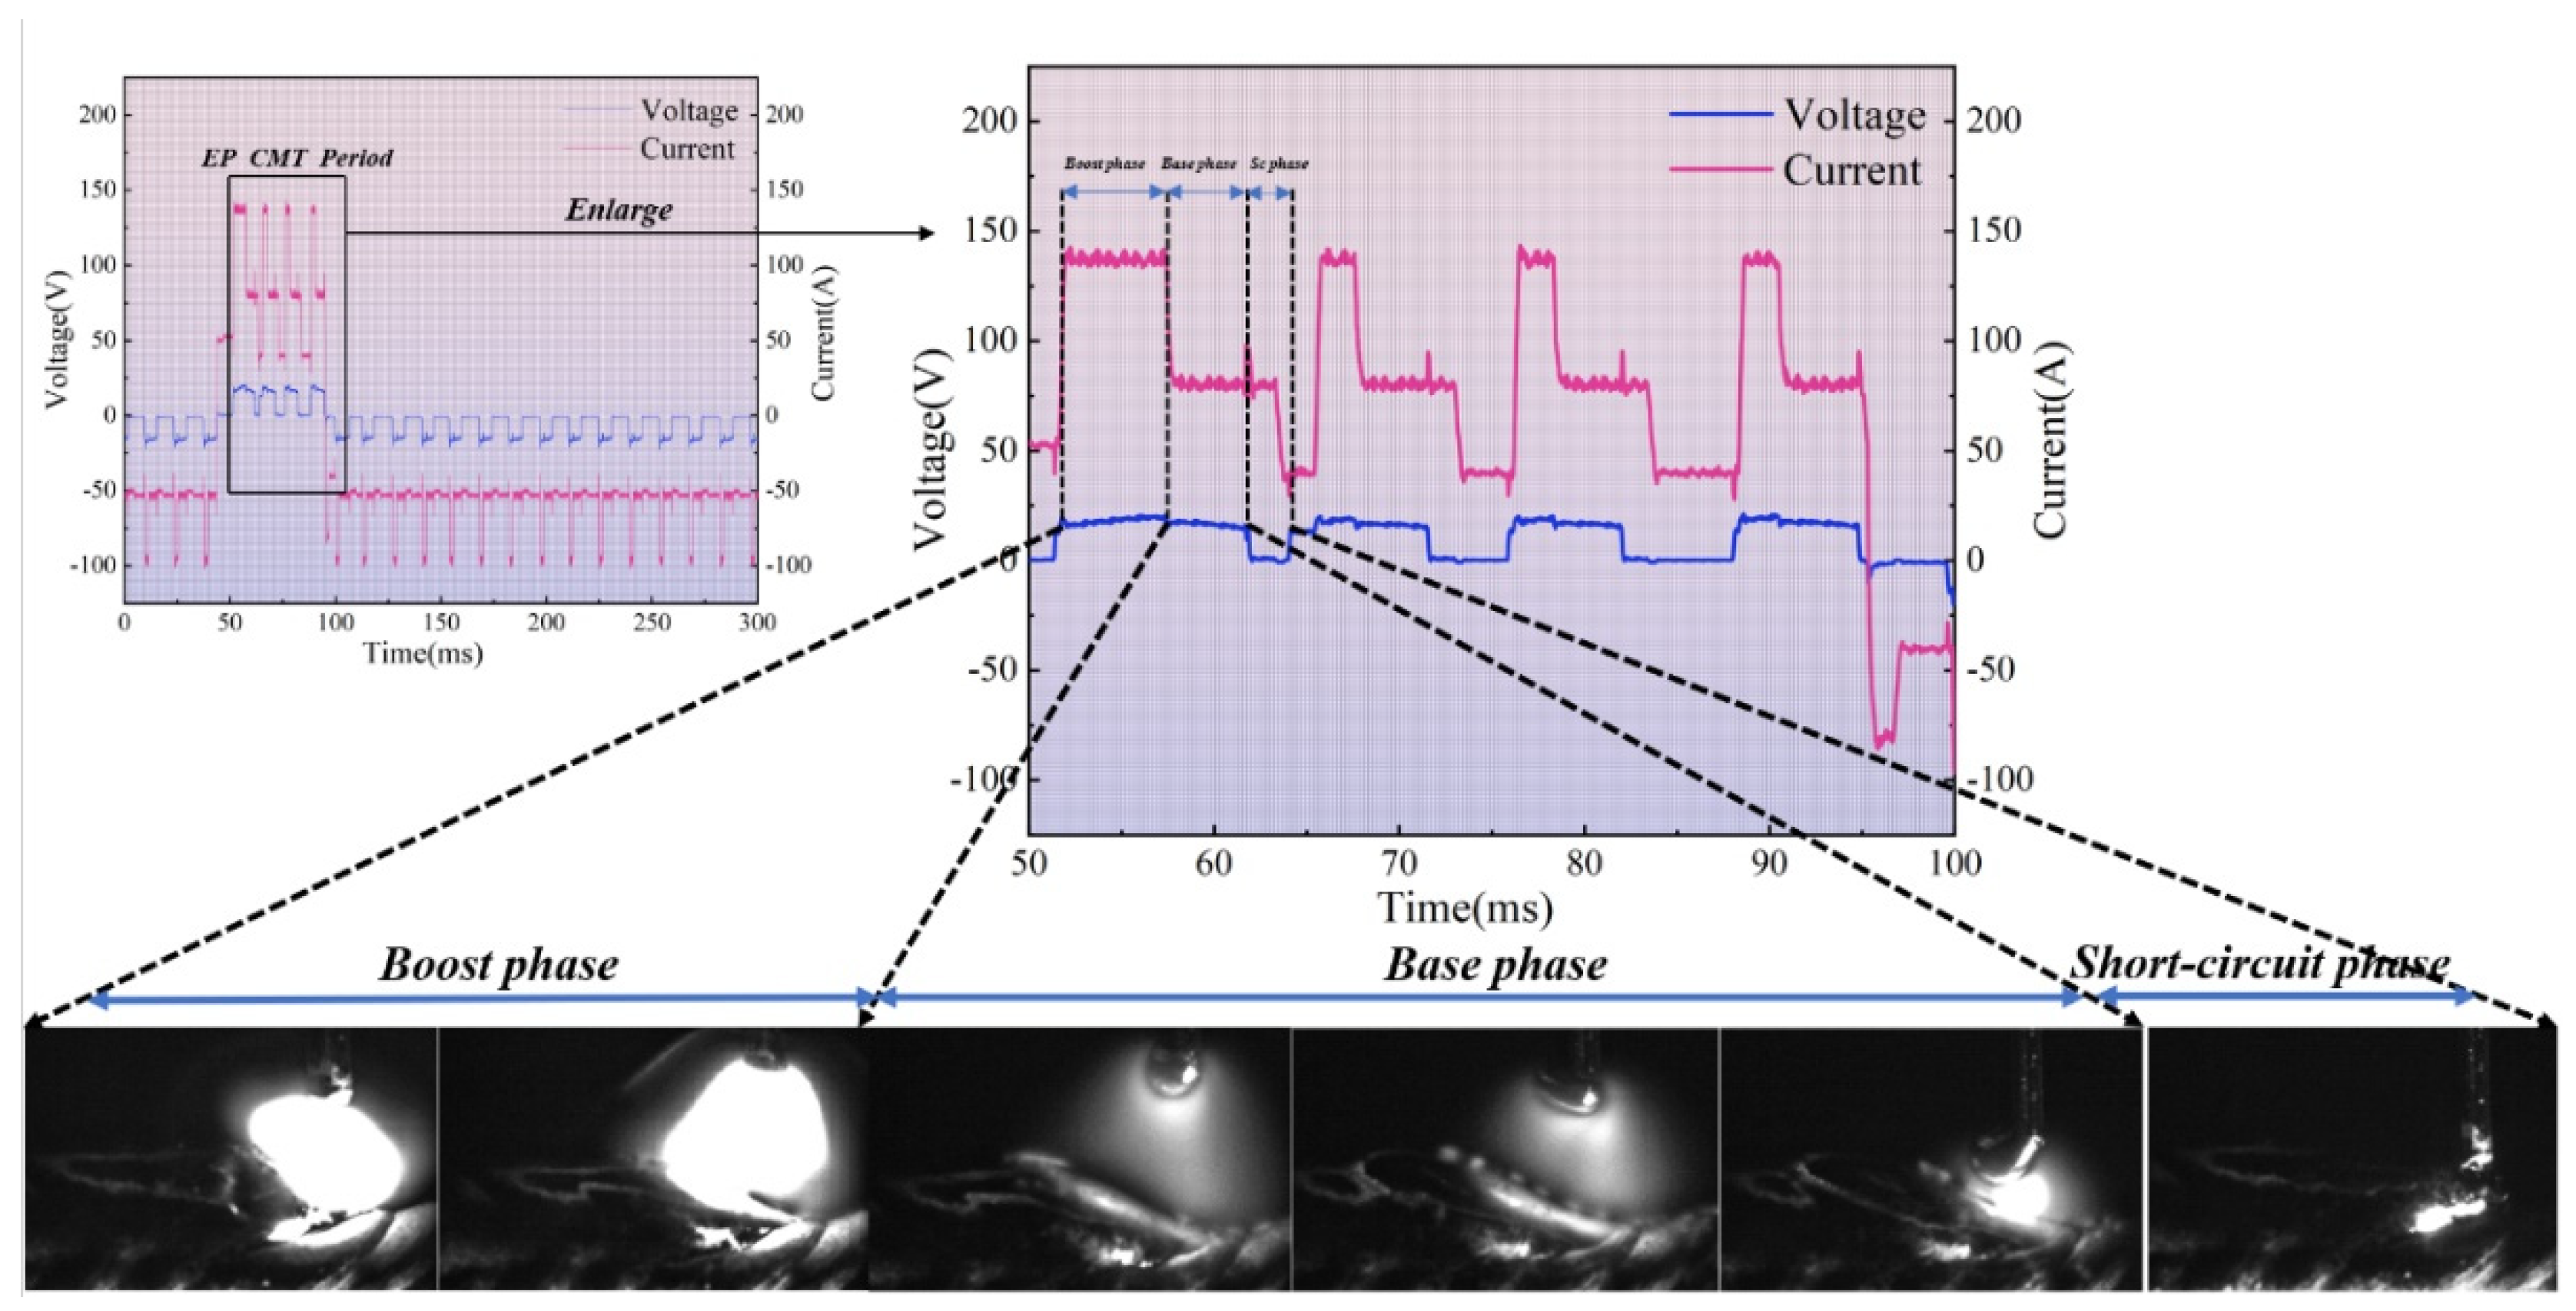
4. Study of Molten Pool Evolution Behaviour in EP/EN Stages of Multi-Layer Single-Pass VP-CMT Process
4.1. Analysis of Molten Pool Velocity Under Different EP:EN Parameters for Multi-Layer Single-Pass Additive Manufacturing
4.2. Variation in Molten Pool Dimensions Under Different EP:EN Parameters
4.3. Changes in Molten Pool Dimensions Under Different EP:EN Parameters
5. Conclusions
- (1)
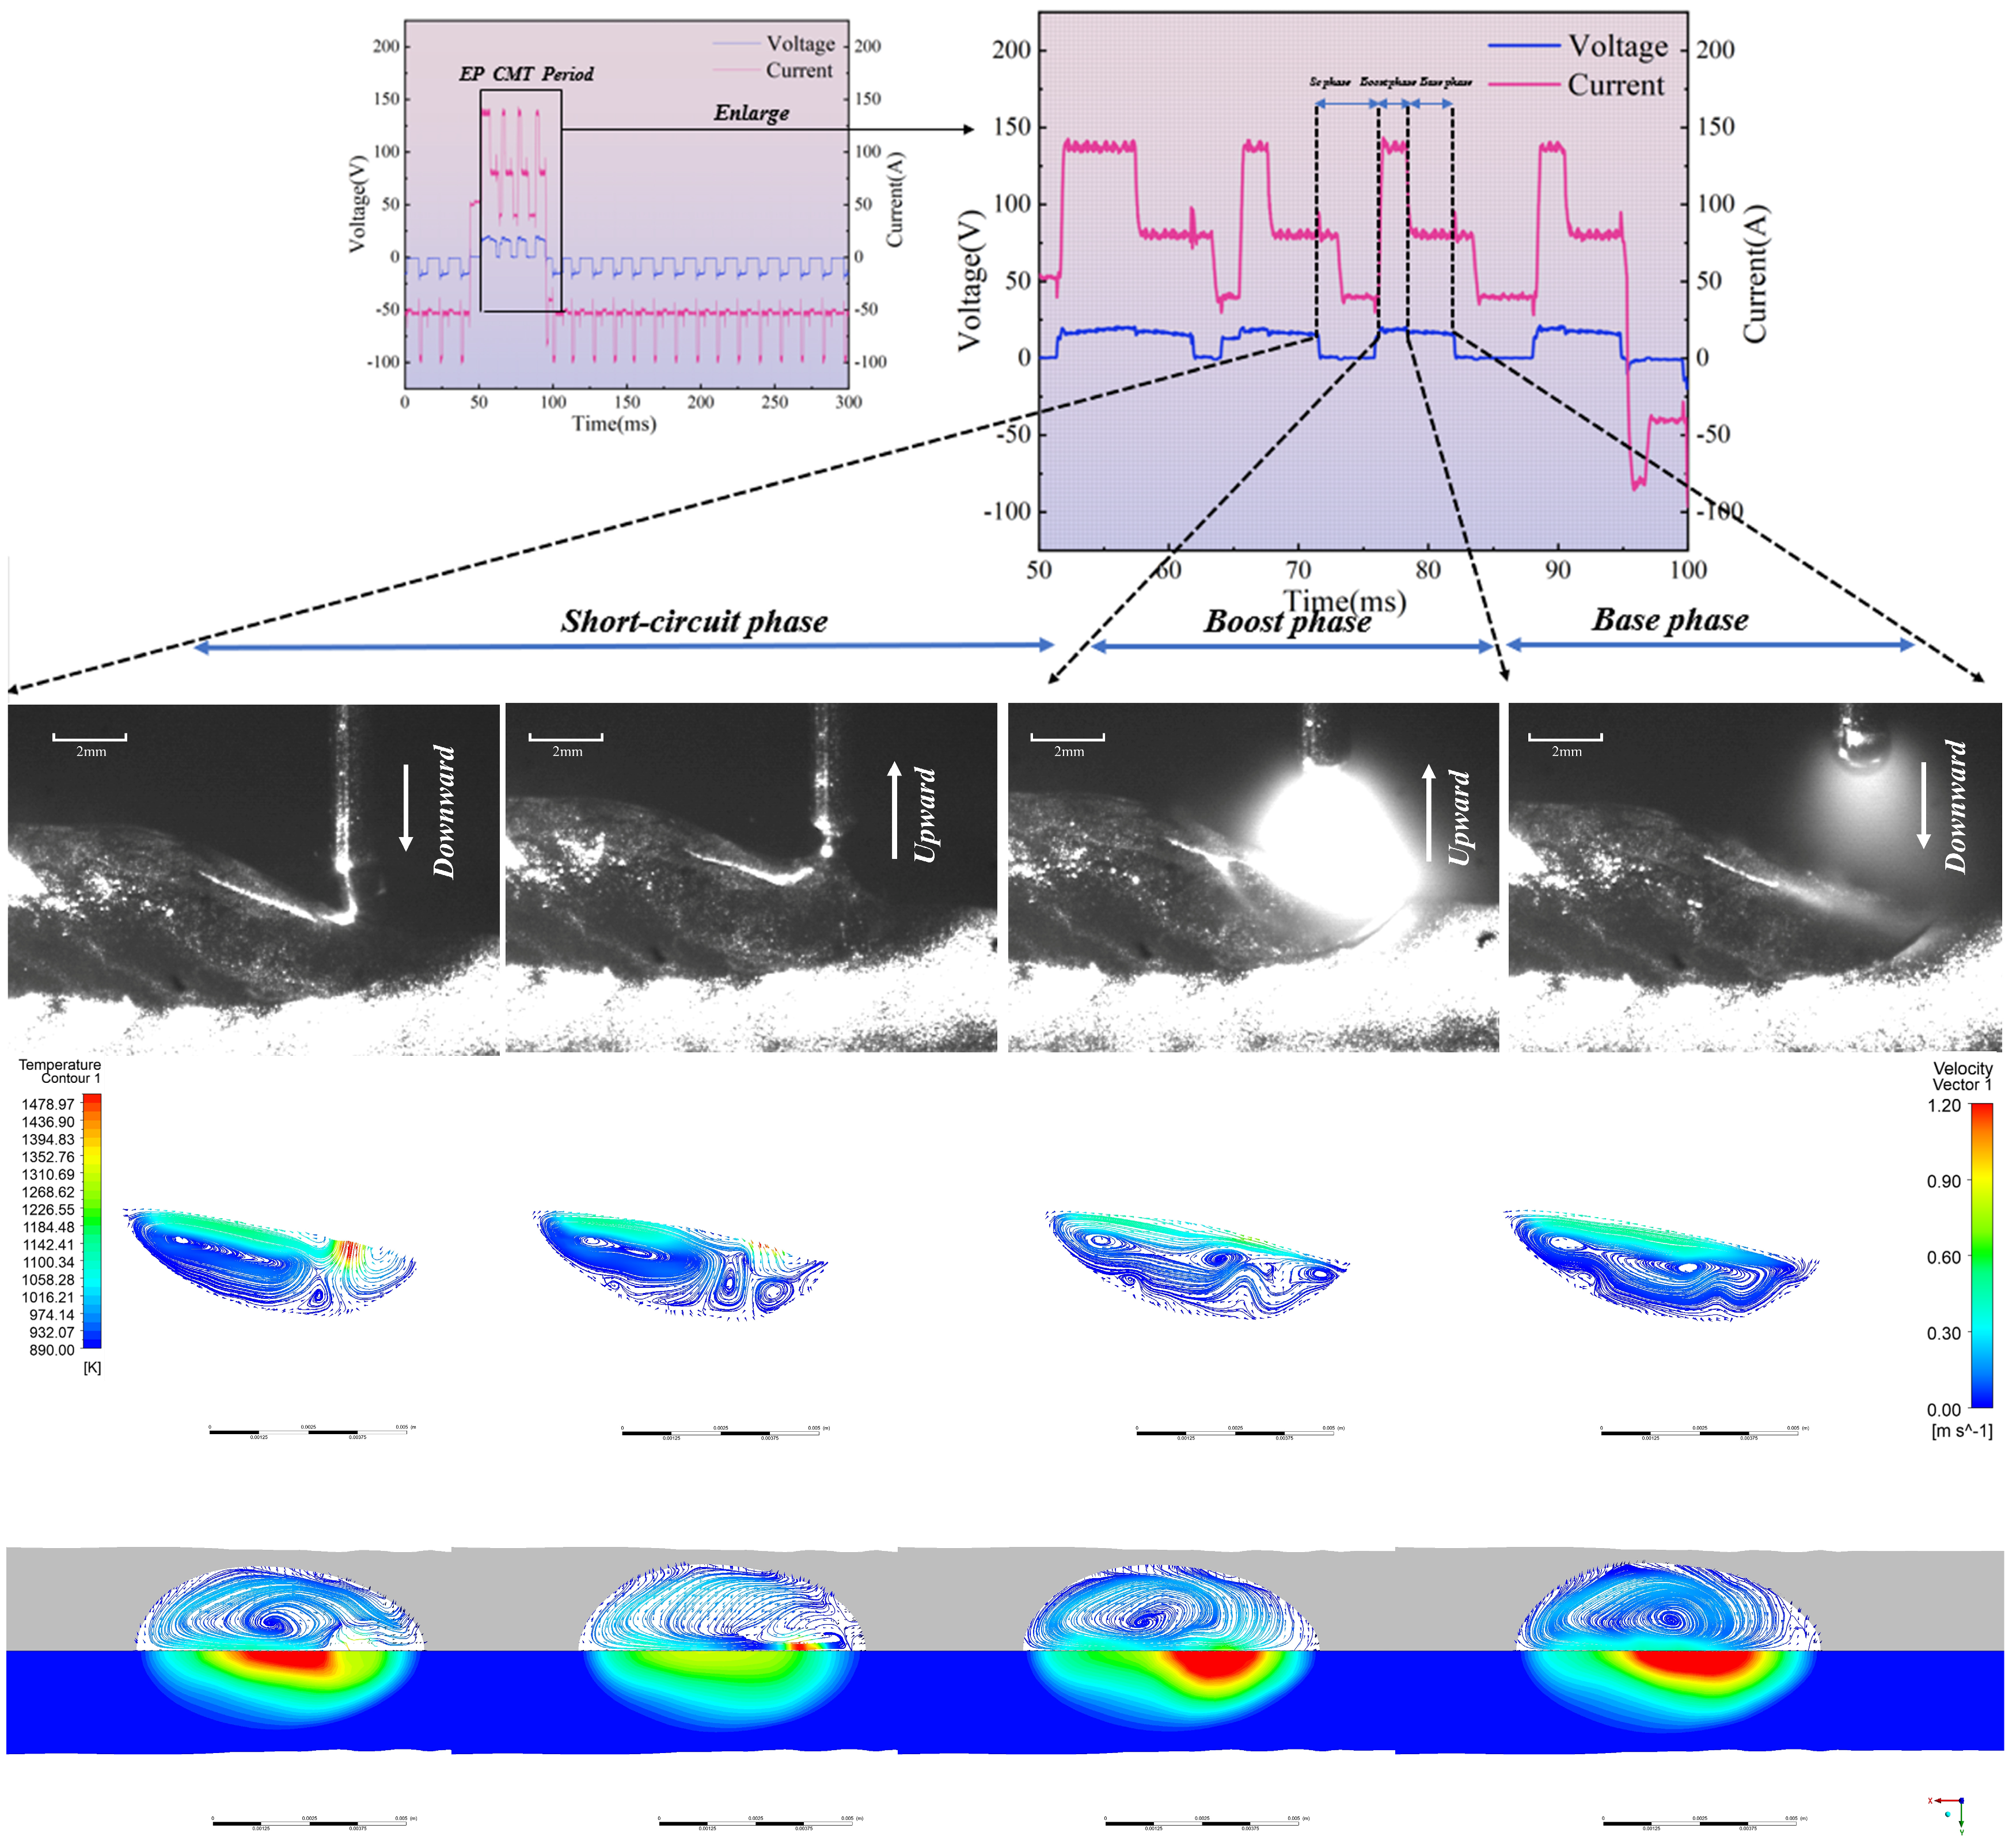
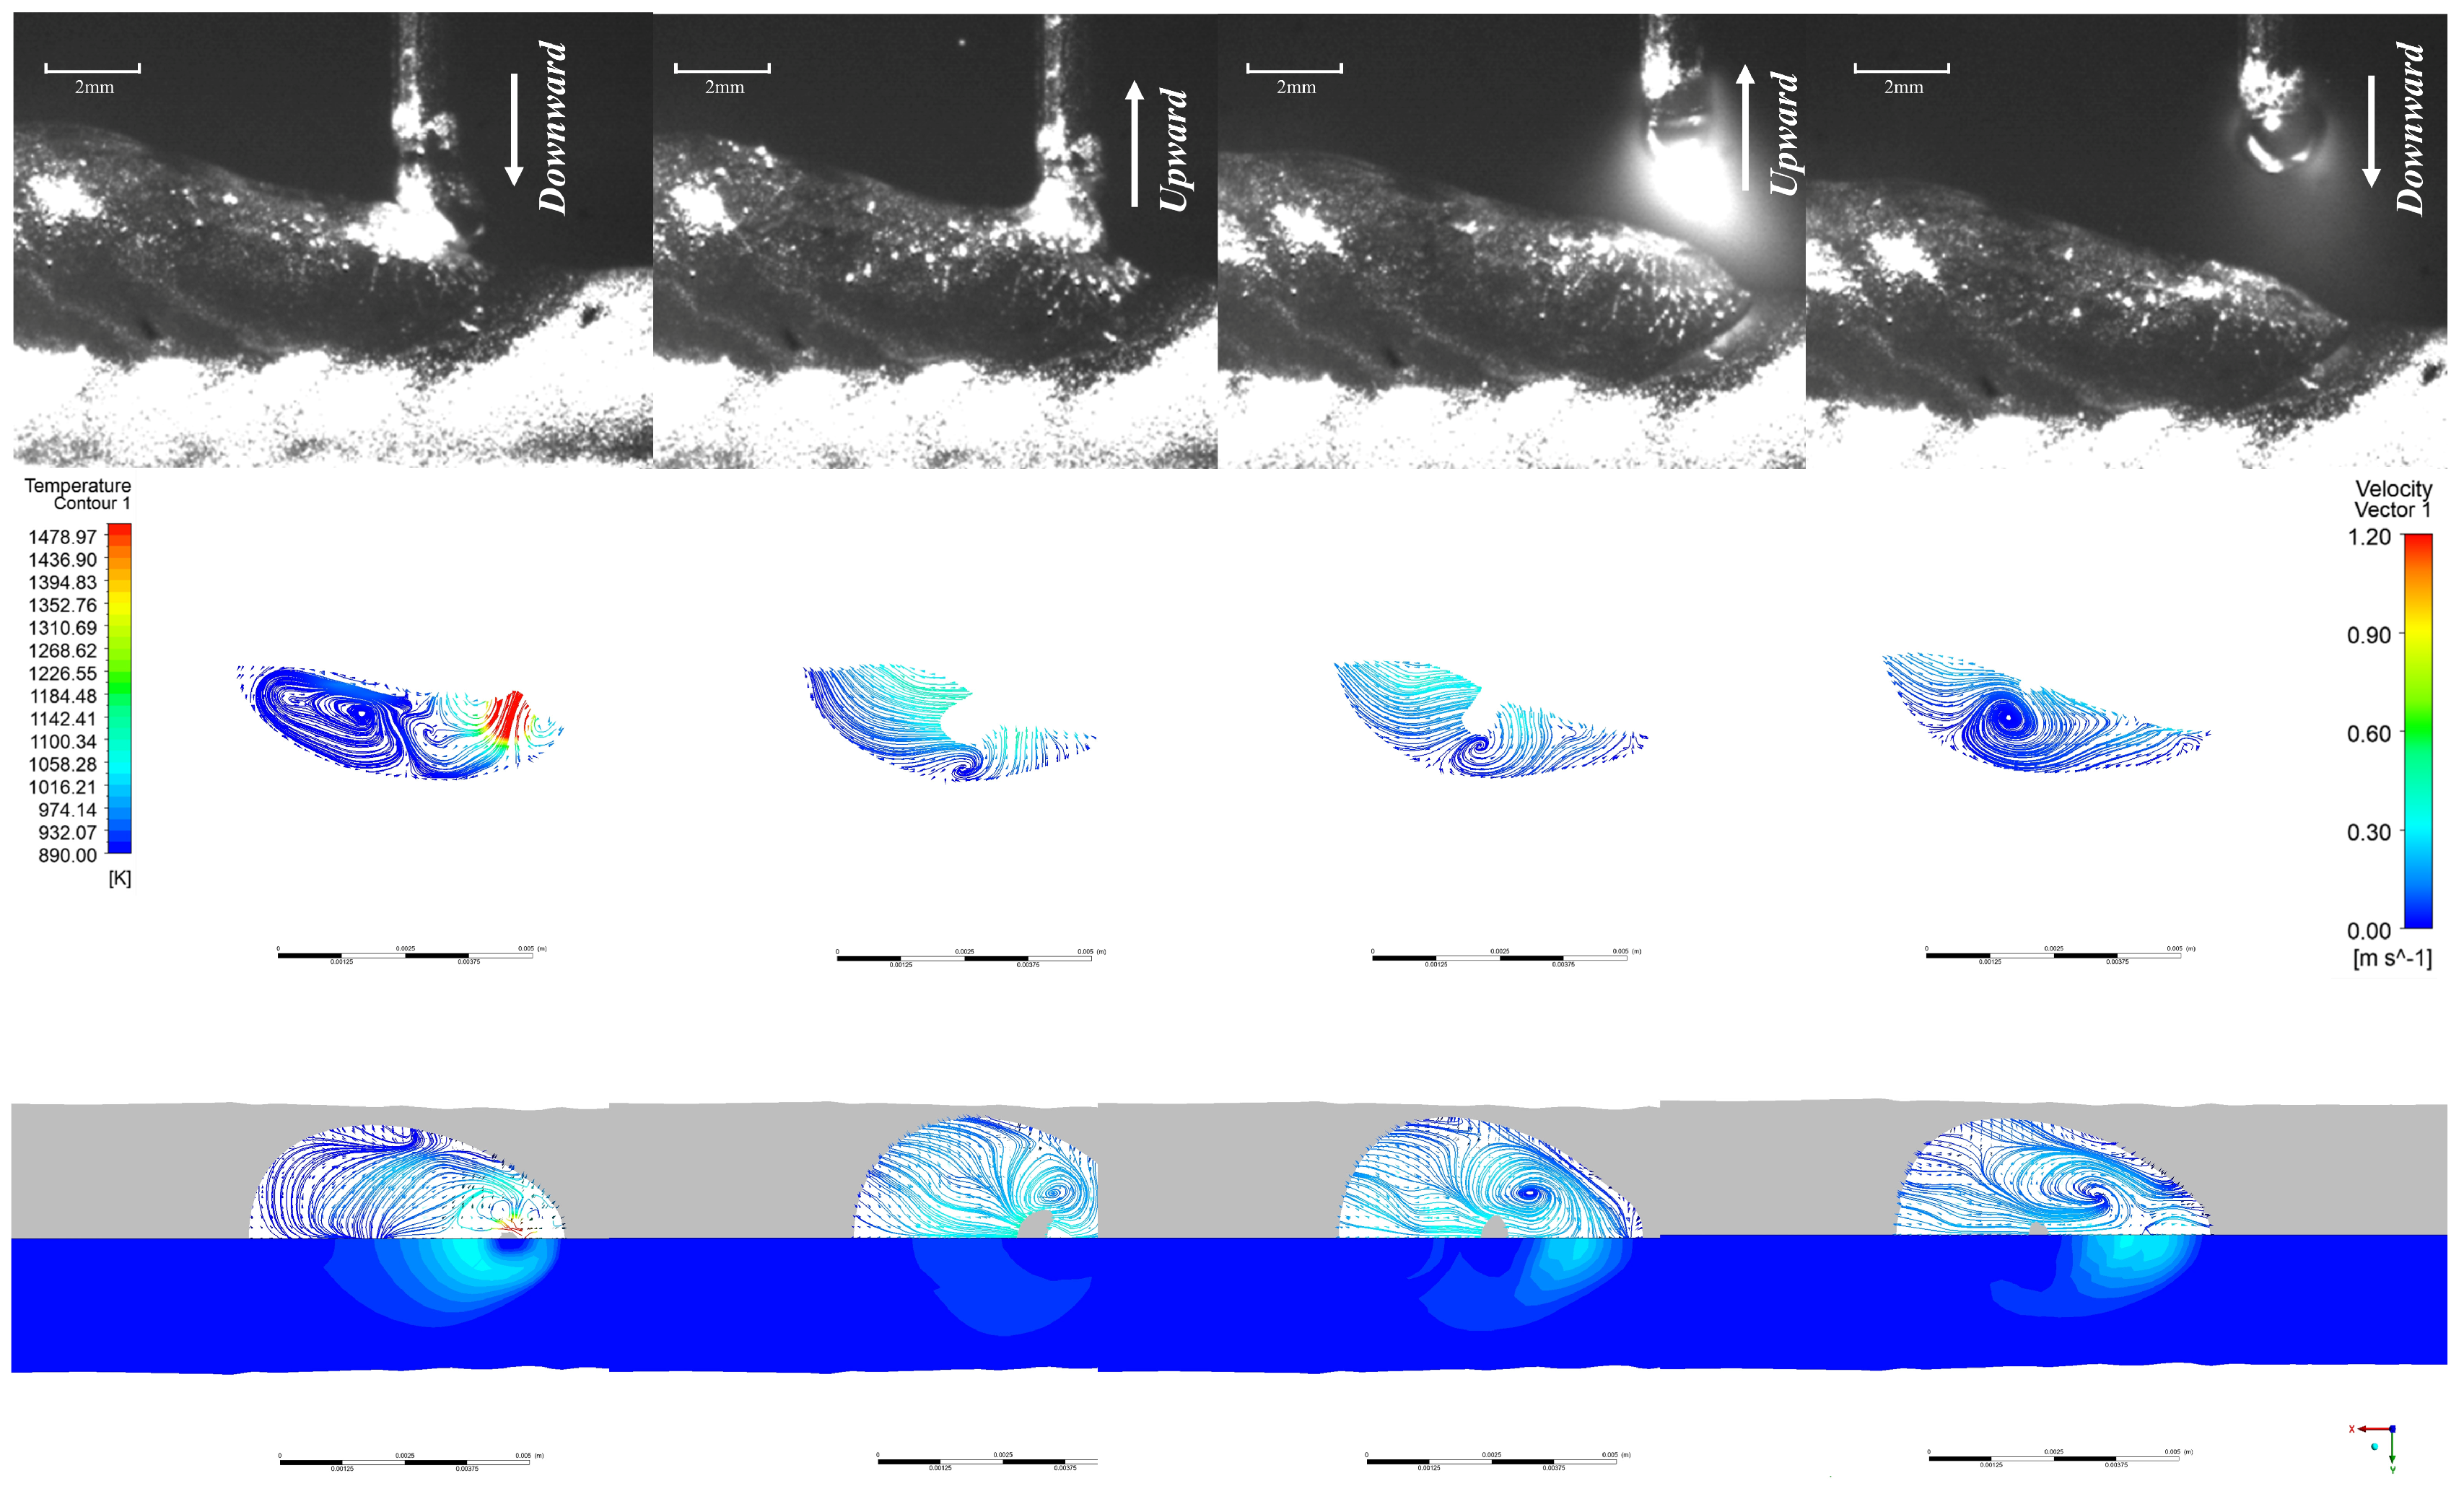
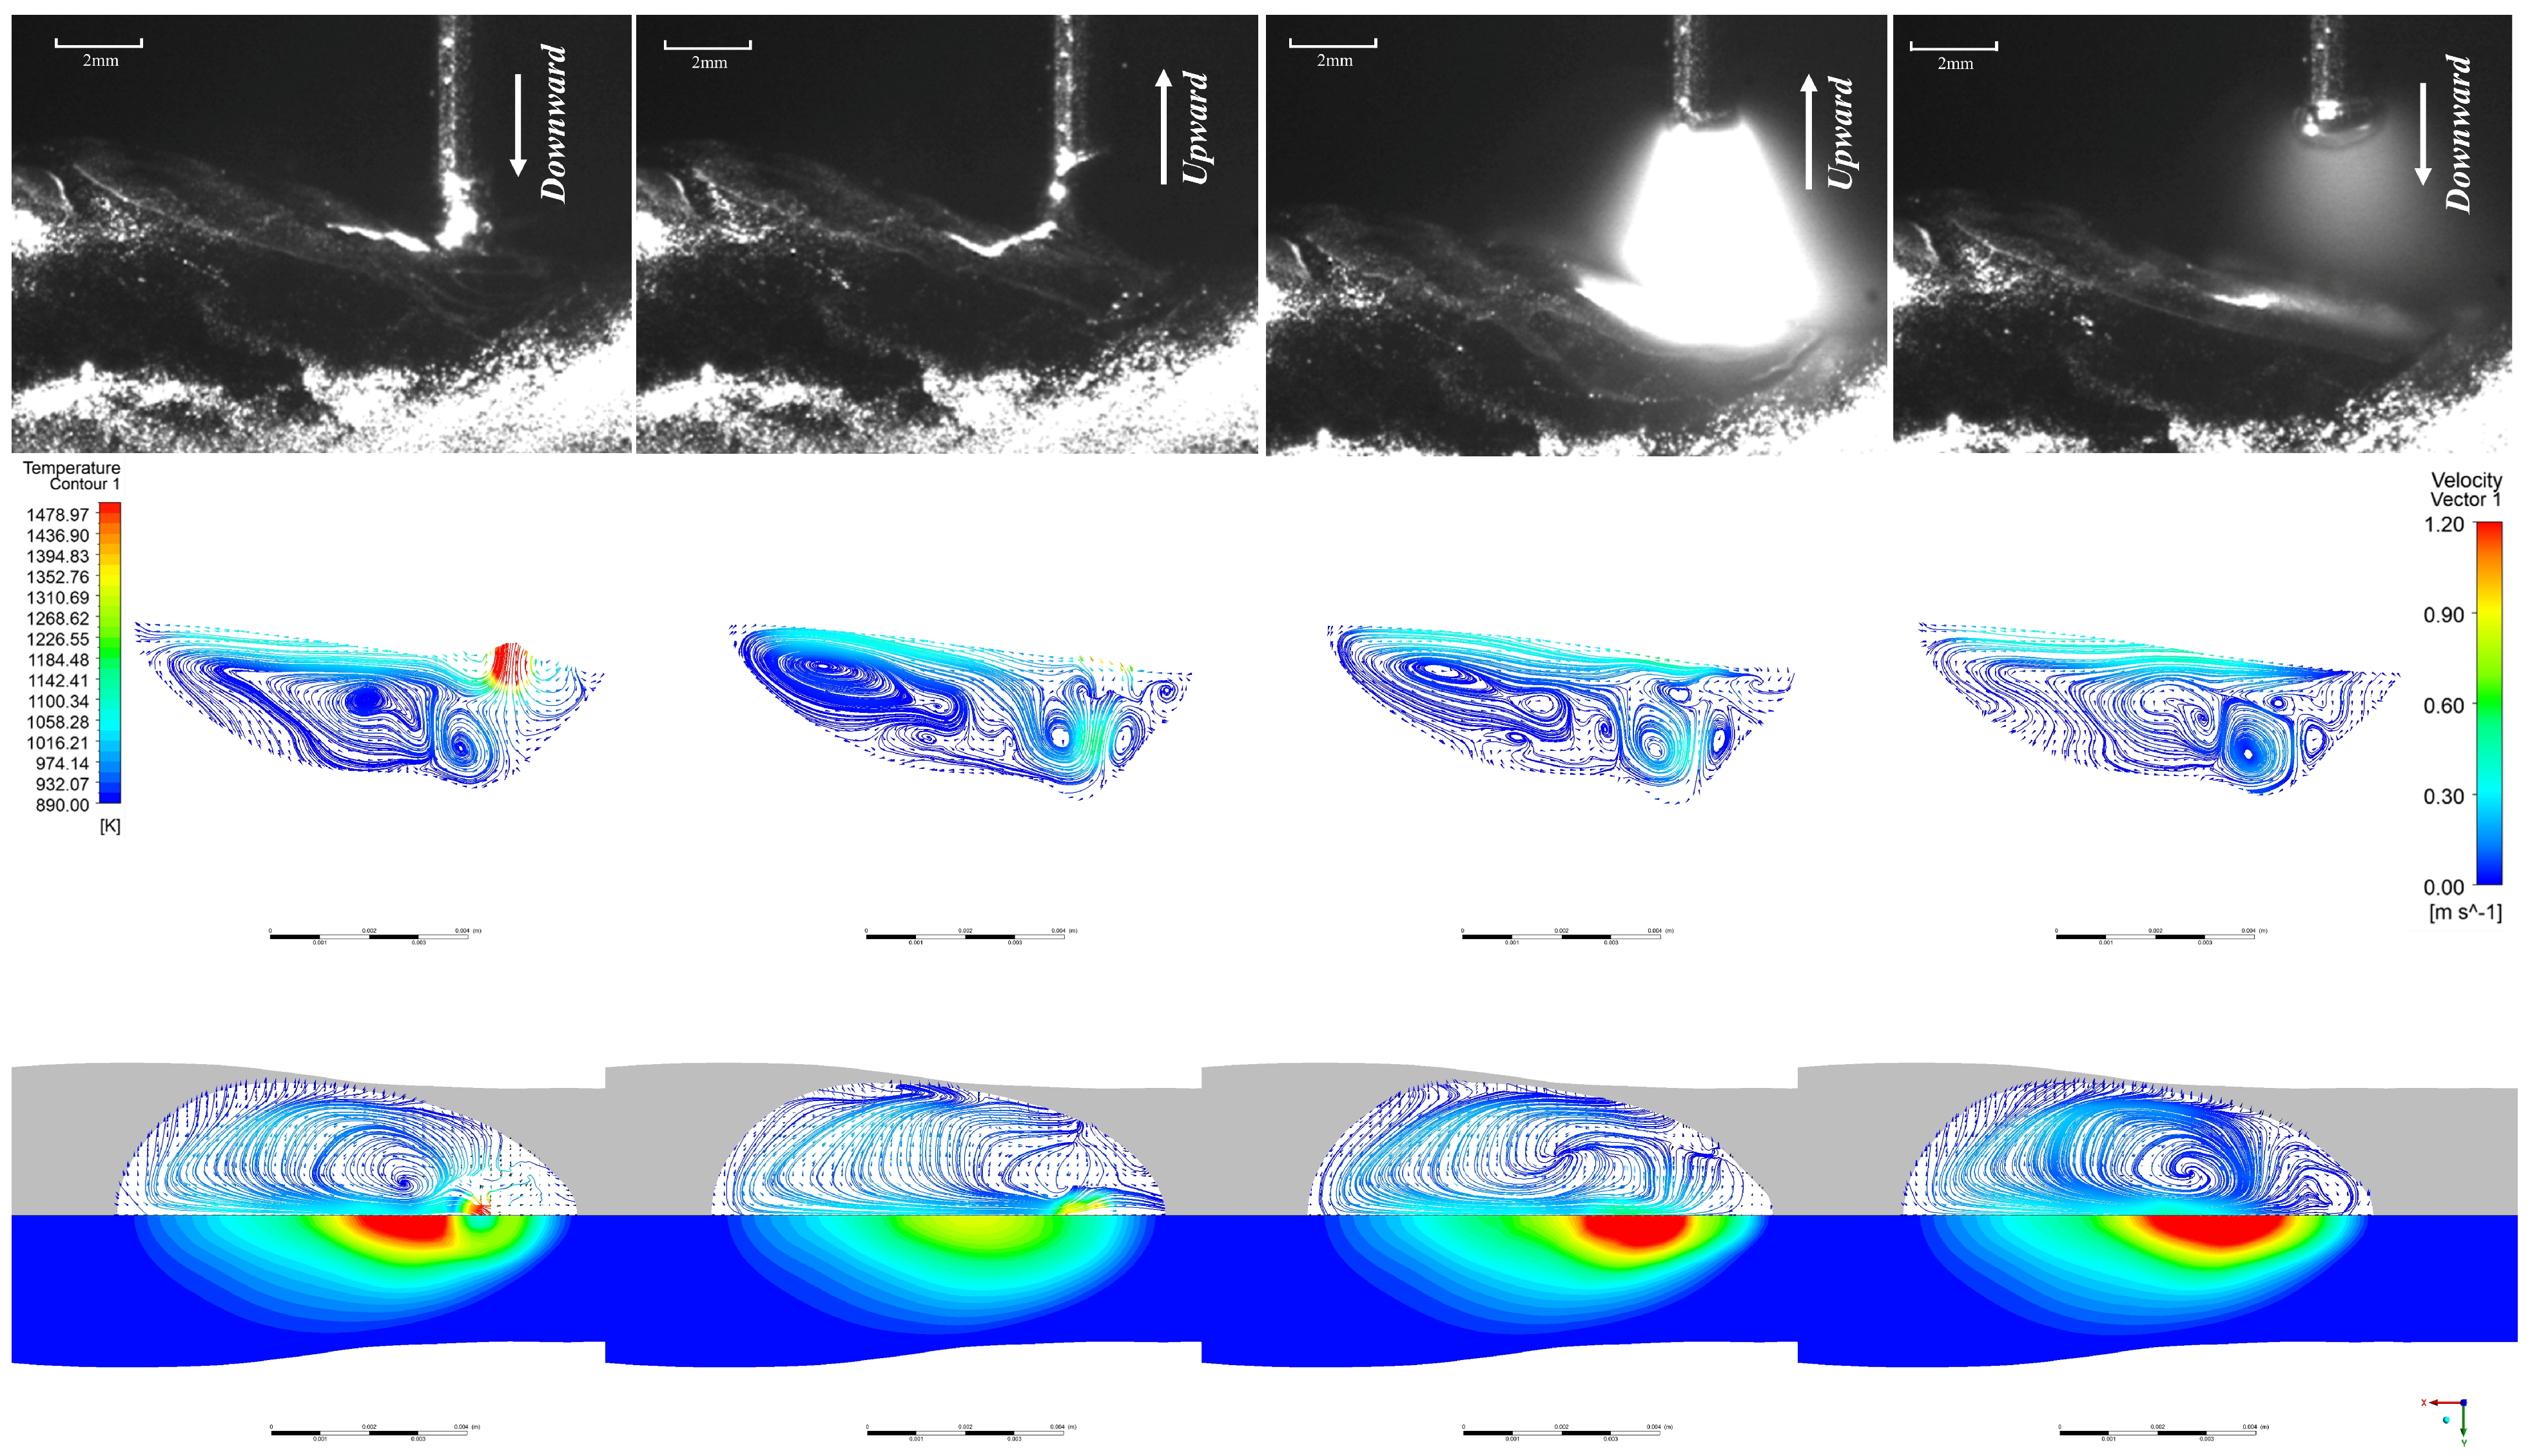
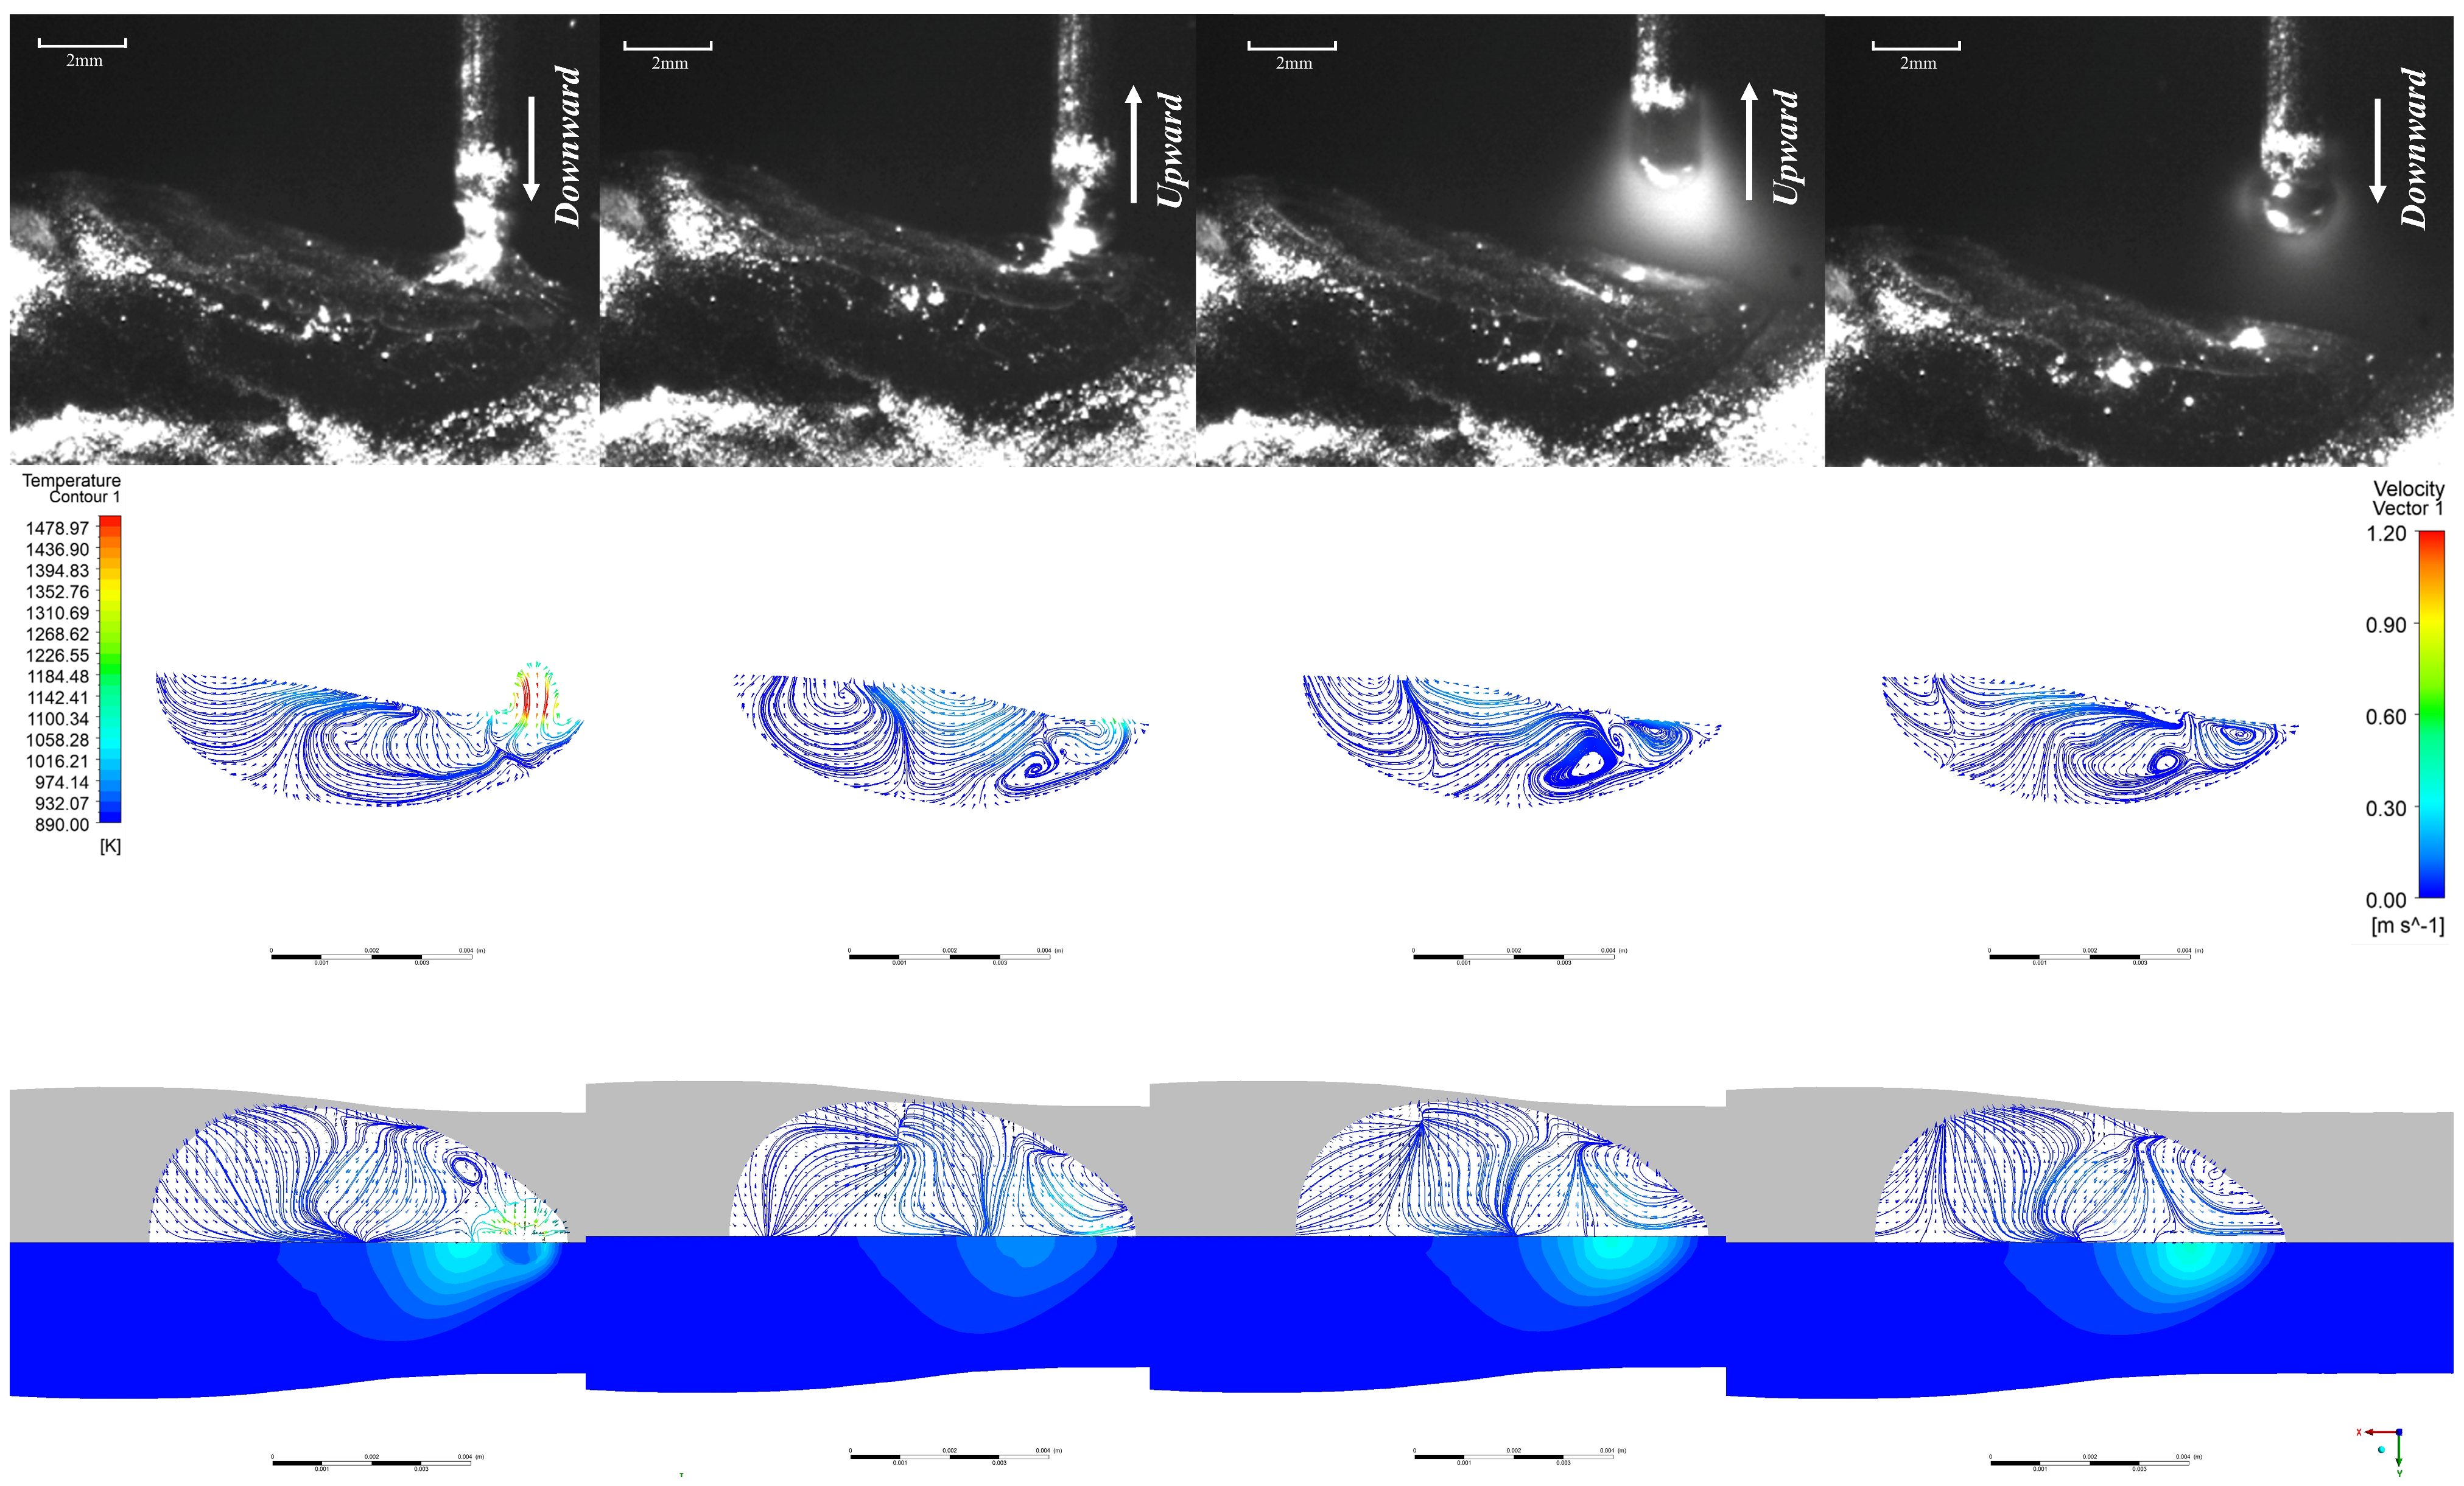
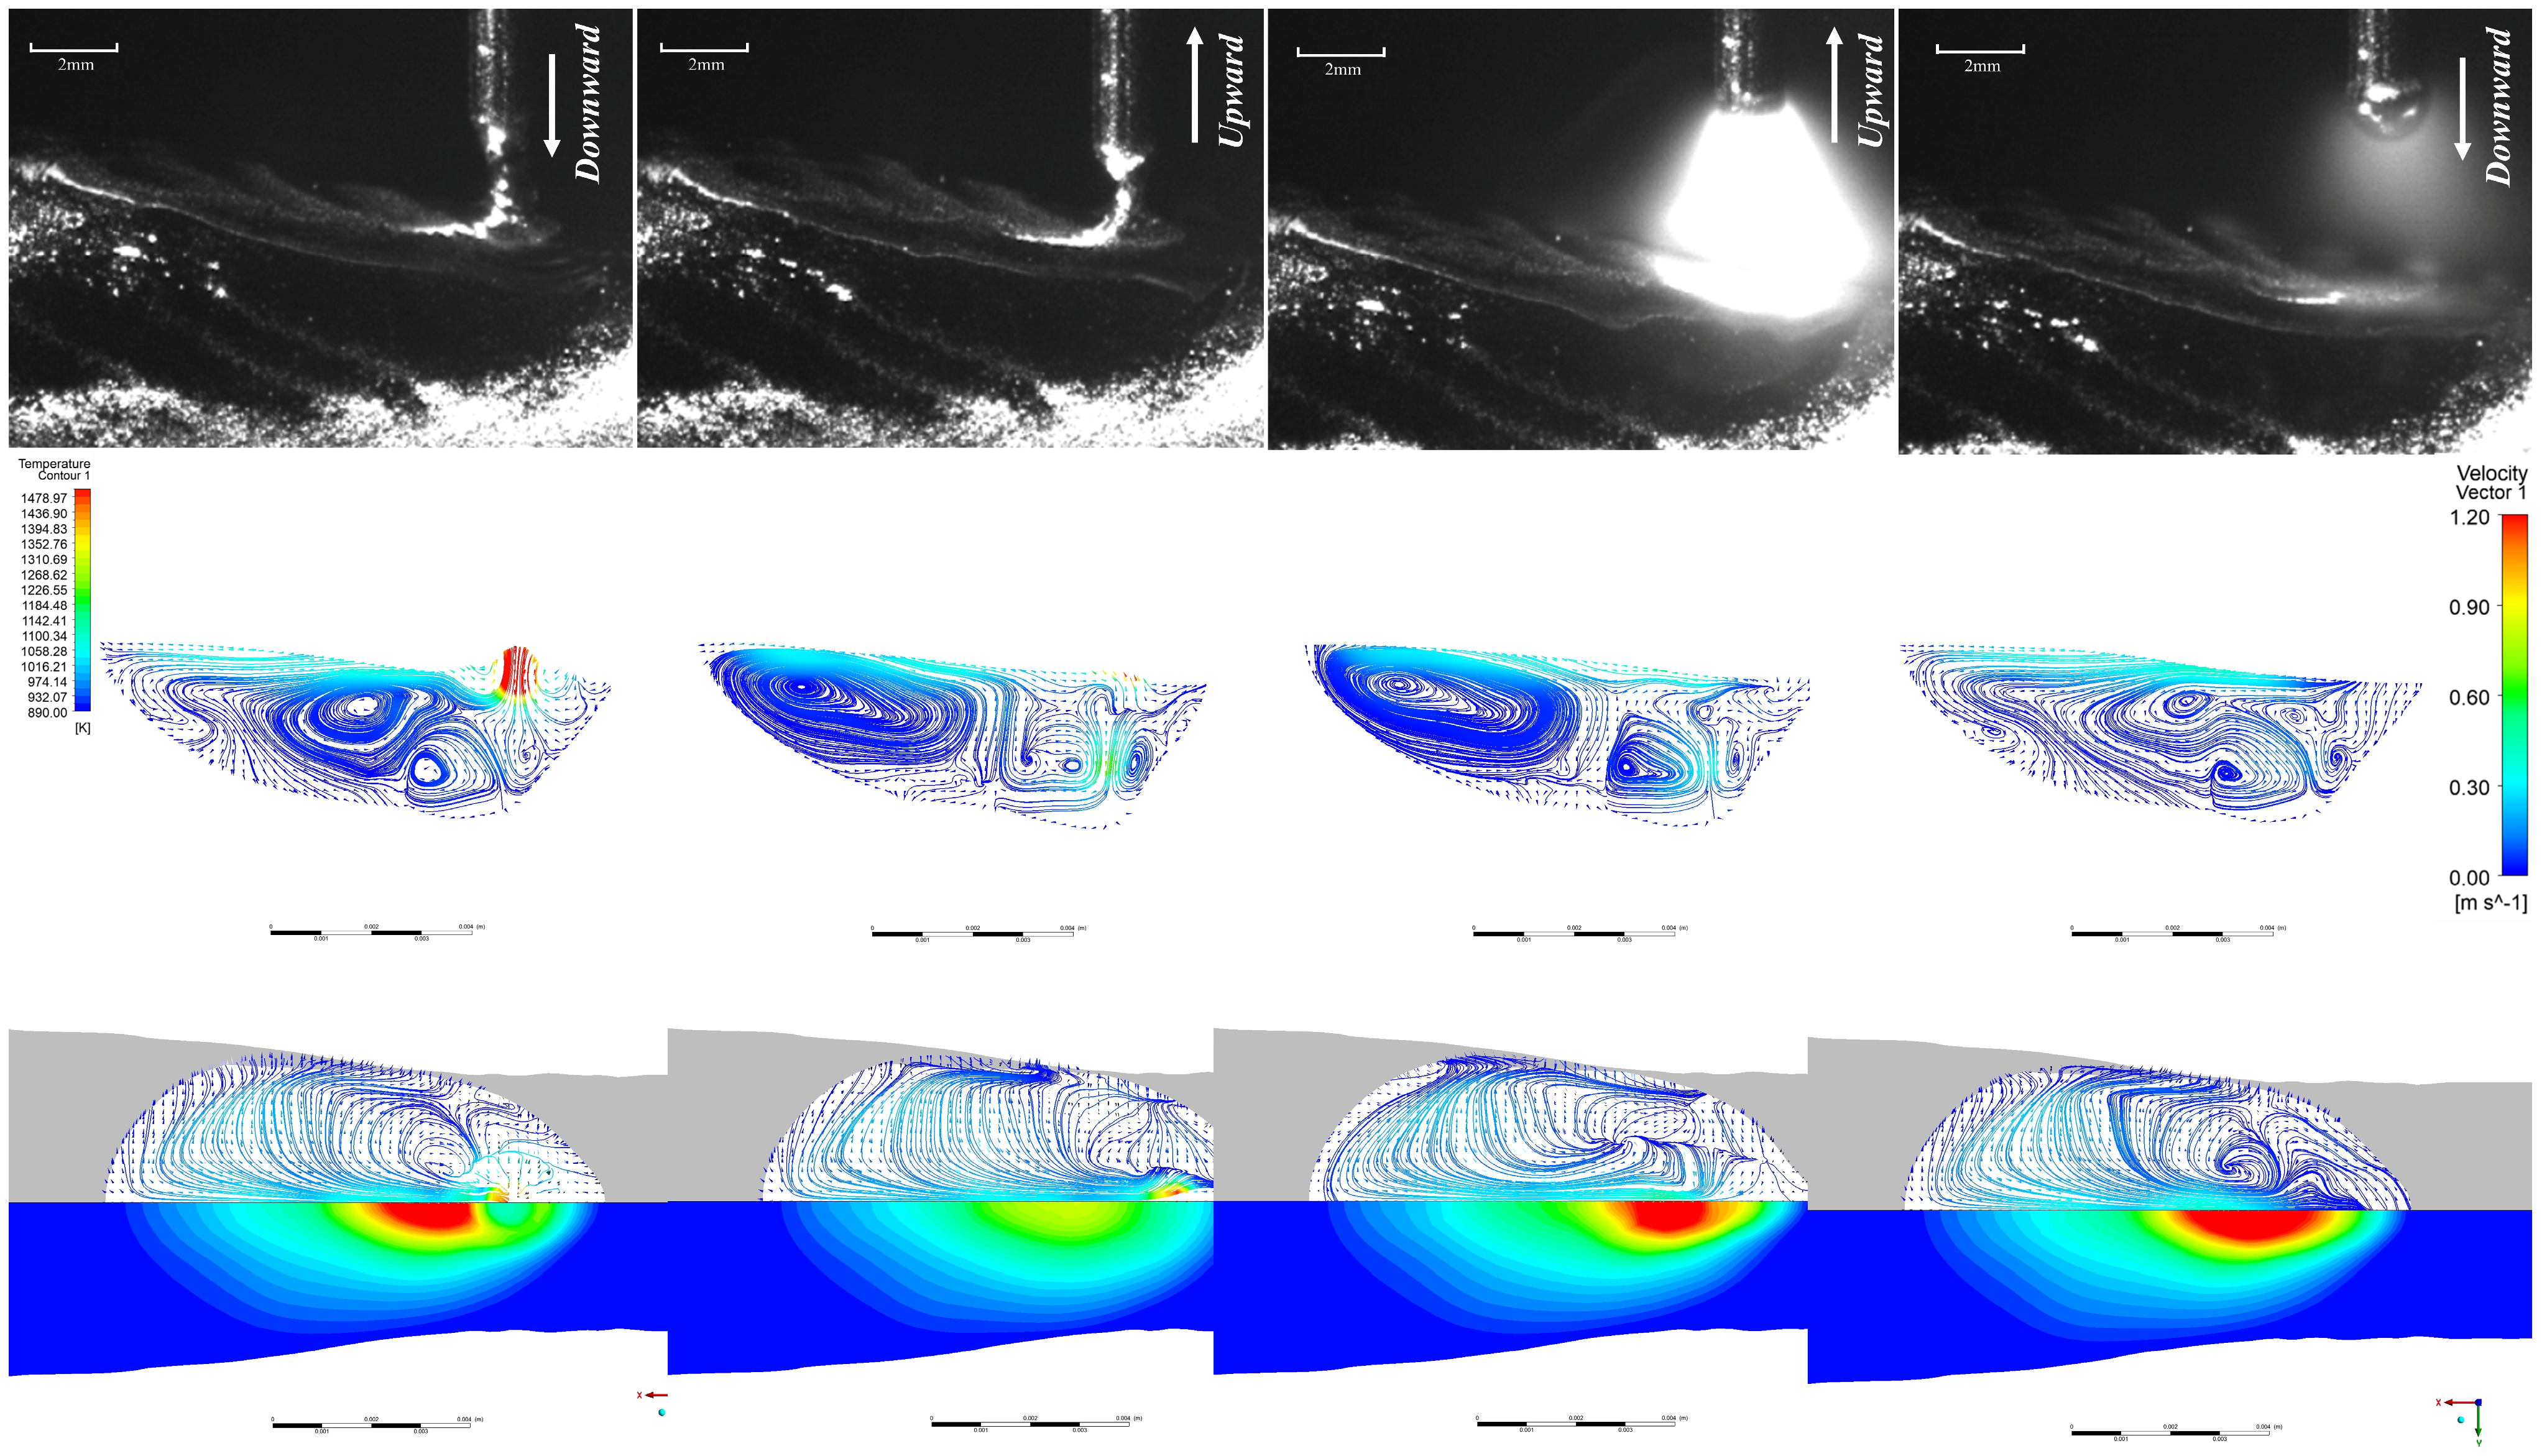
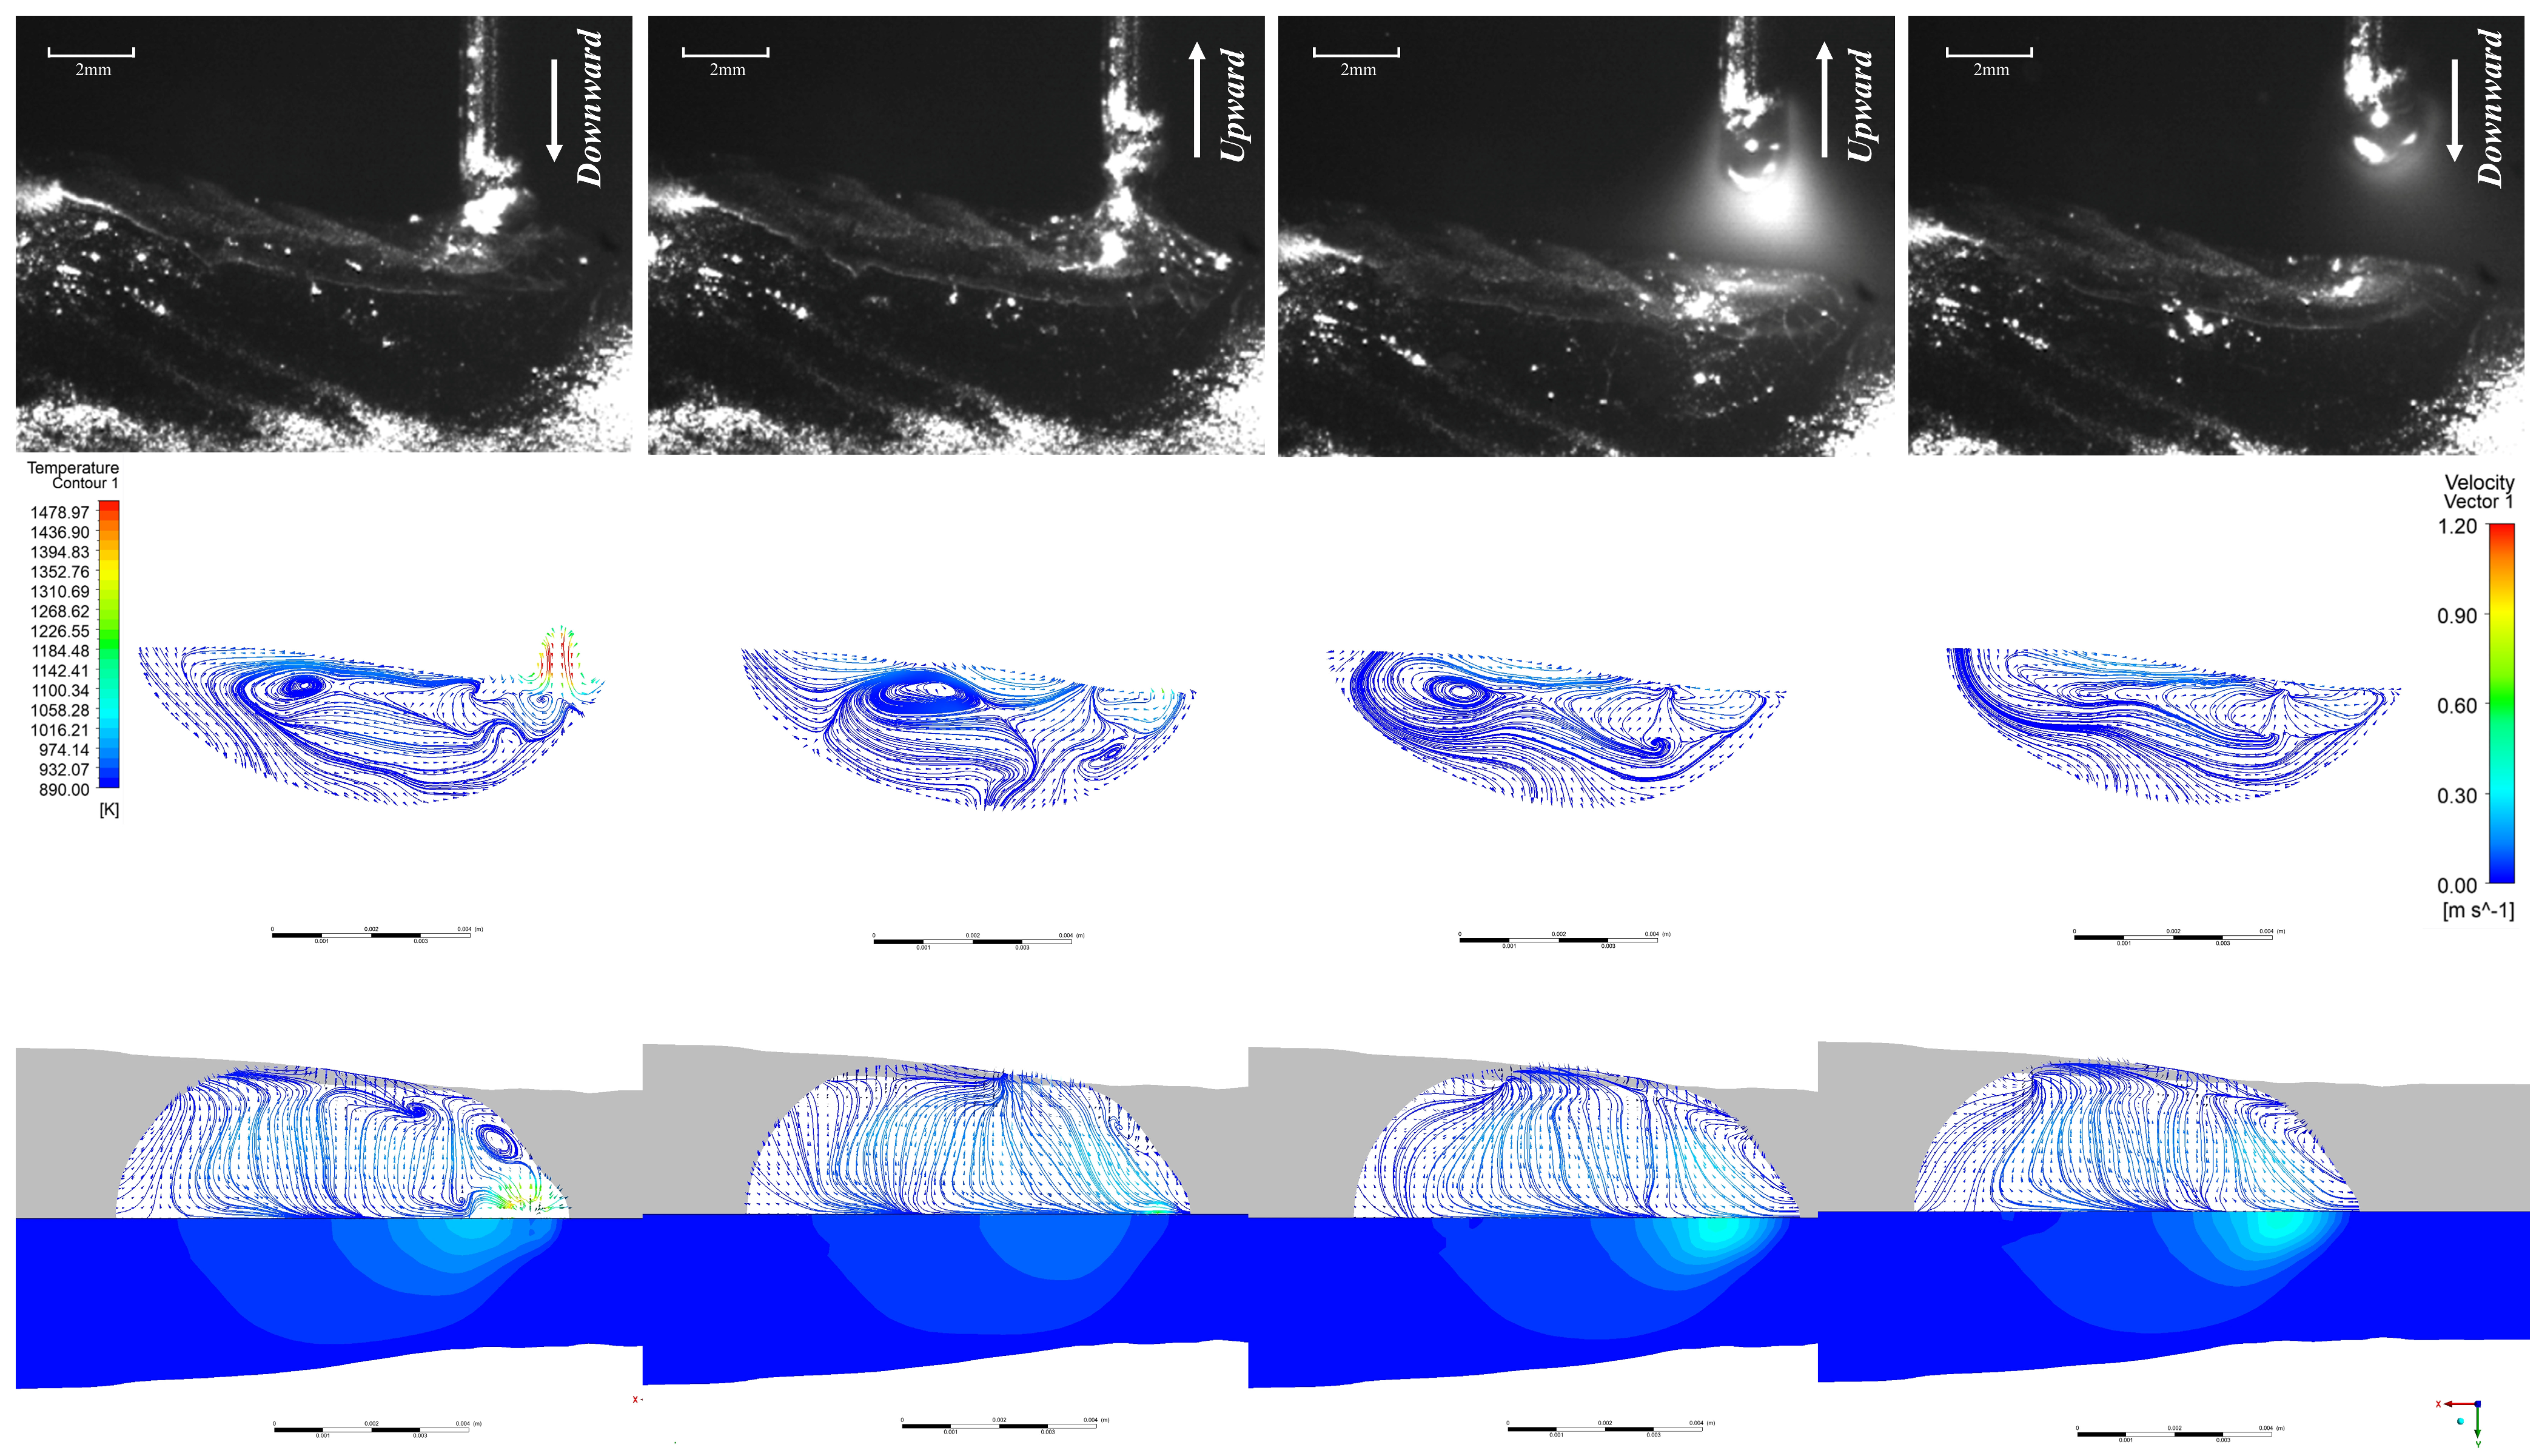
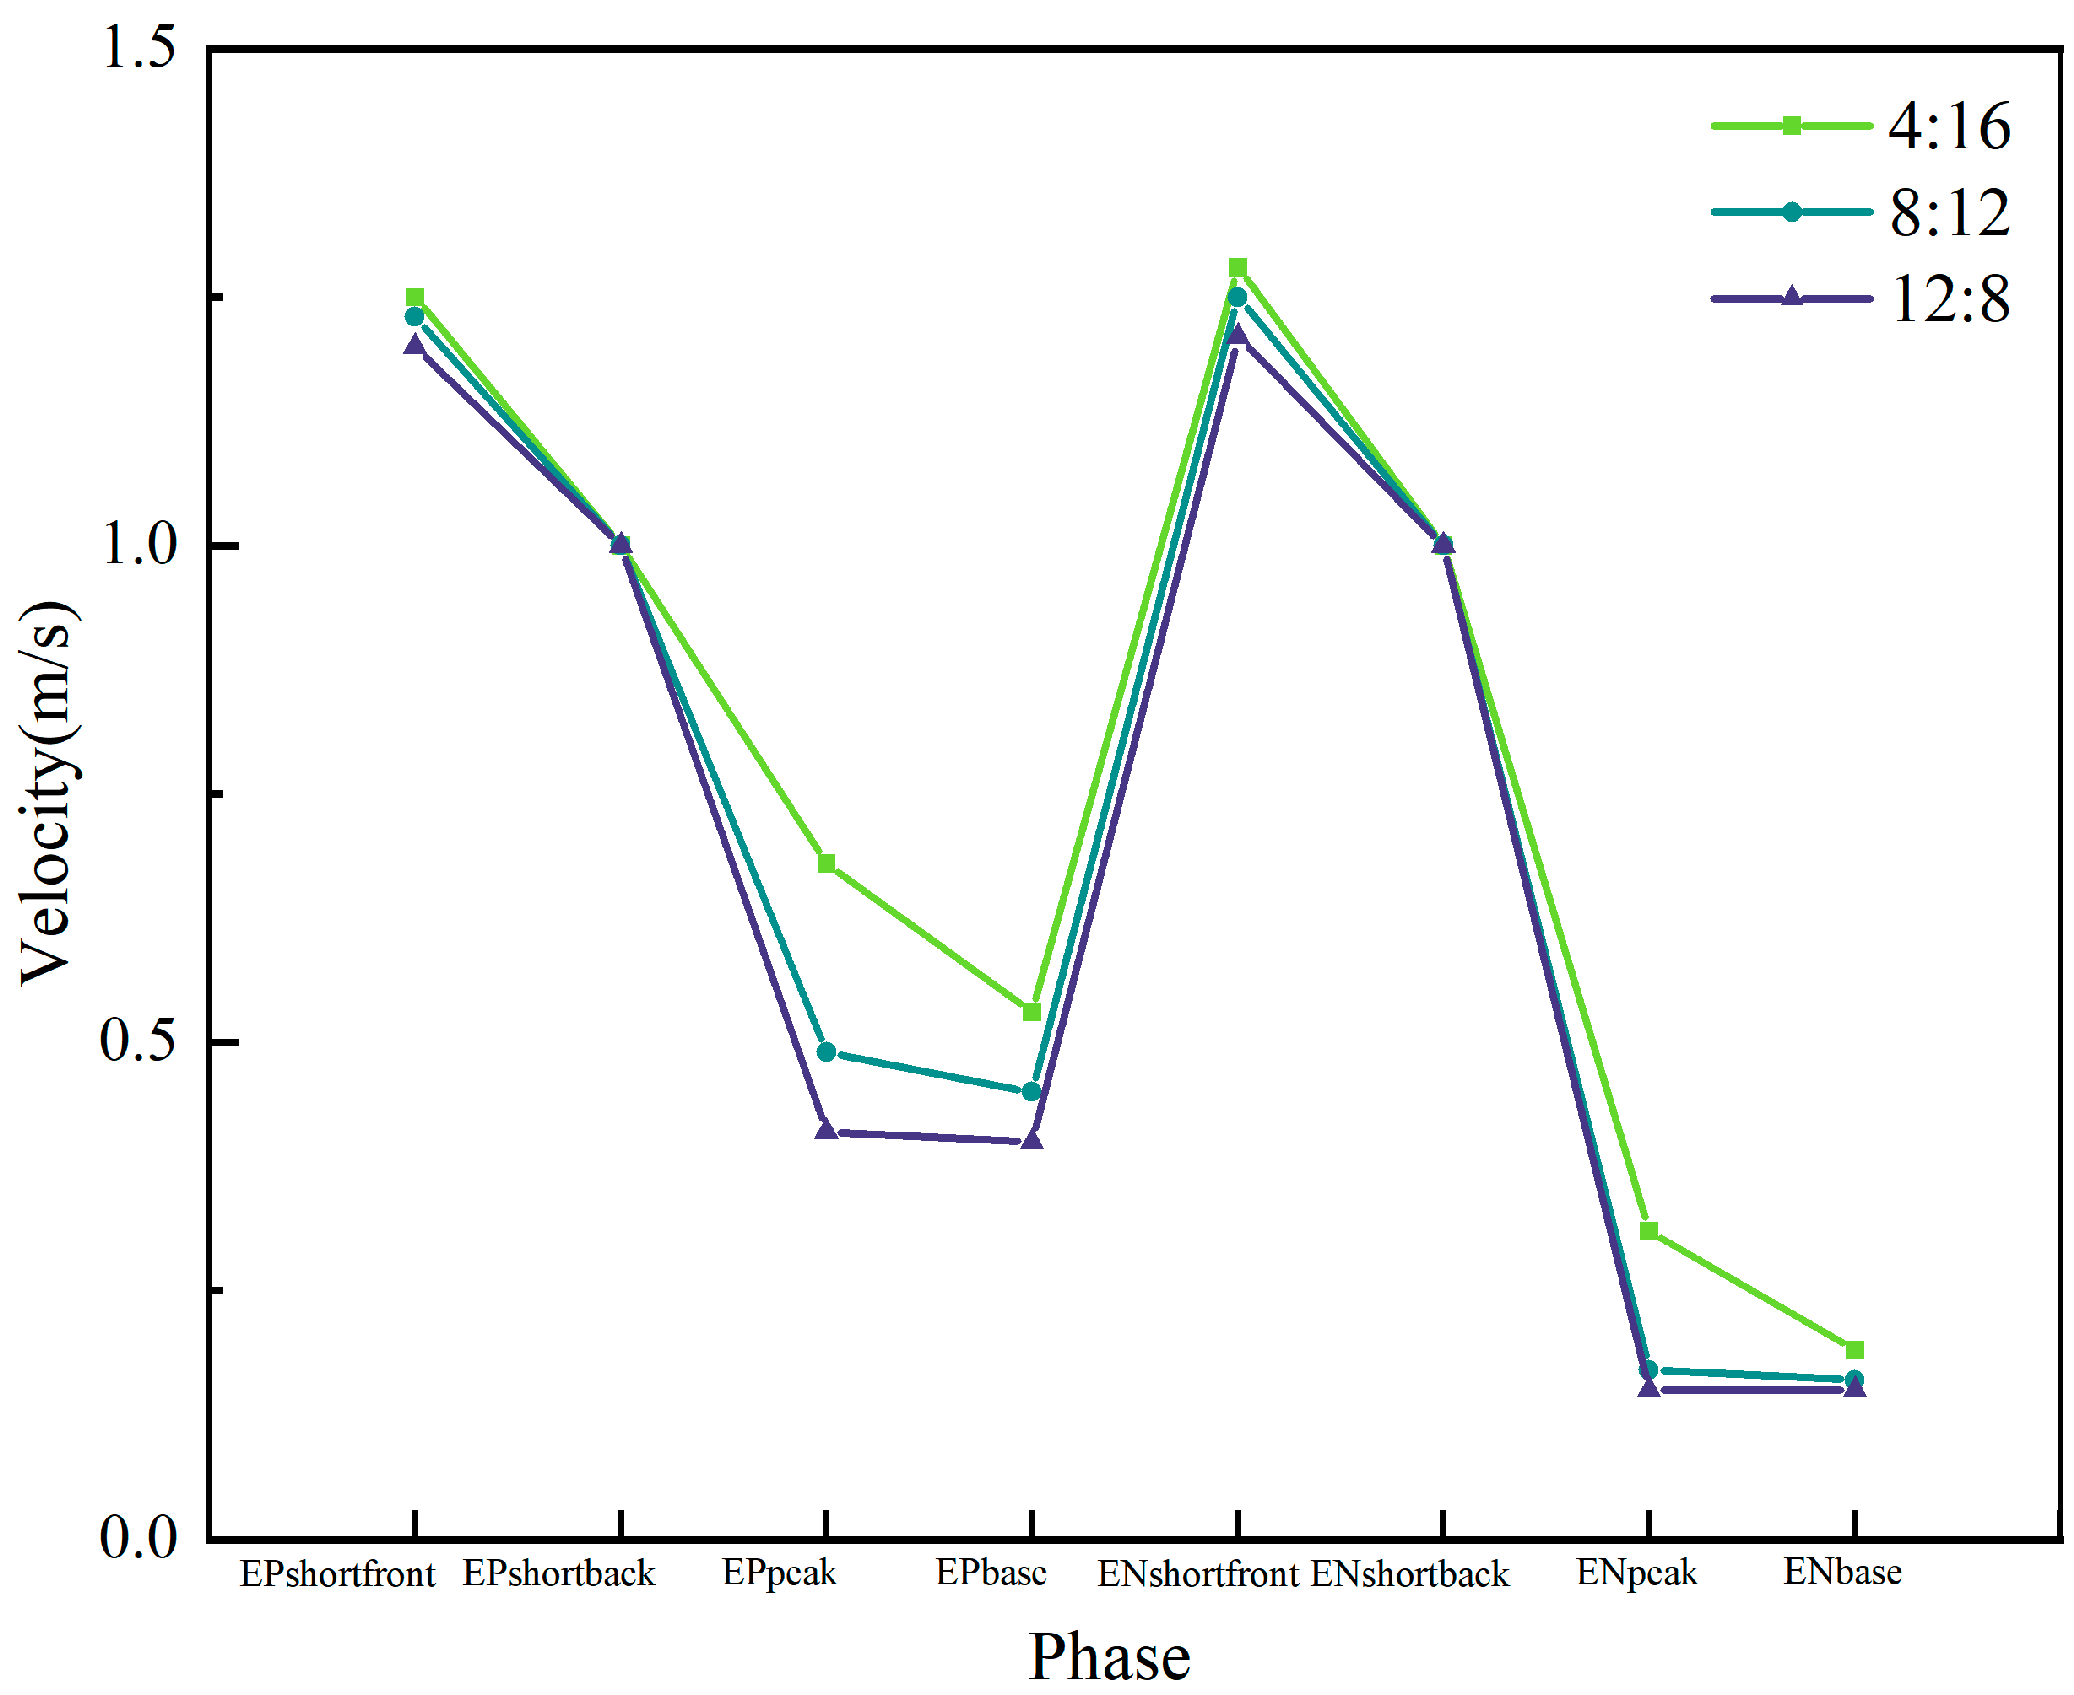
- Molten pool flow behaviour is dominated by Marangoni forces, with significantly higher flow velocities during the EP phase. Simulations indicate that surface flow is primarily driven by Marangoni forces induced by temperature gradients. During the EP phase, arc divergence, high heat input, and extensive arc pressure influence result in intense internal flow, with peak velocities reaching 0.68 m/s. In contrast, the EN phase features a concentrated arc, weaker thermal effects, and lower flow velocities. As the EP proportion increases (4:16 → 12:8), the overall bath temperature rises, the temperature difference between droplets and the bath decreases, and the Marangoni force weakens. Consequently, the peak flow velocity during the EP phase exhibits a decreasing trend.
- (2)
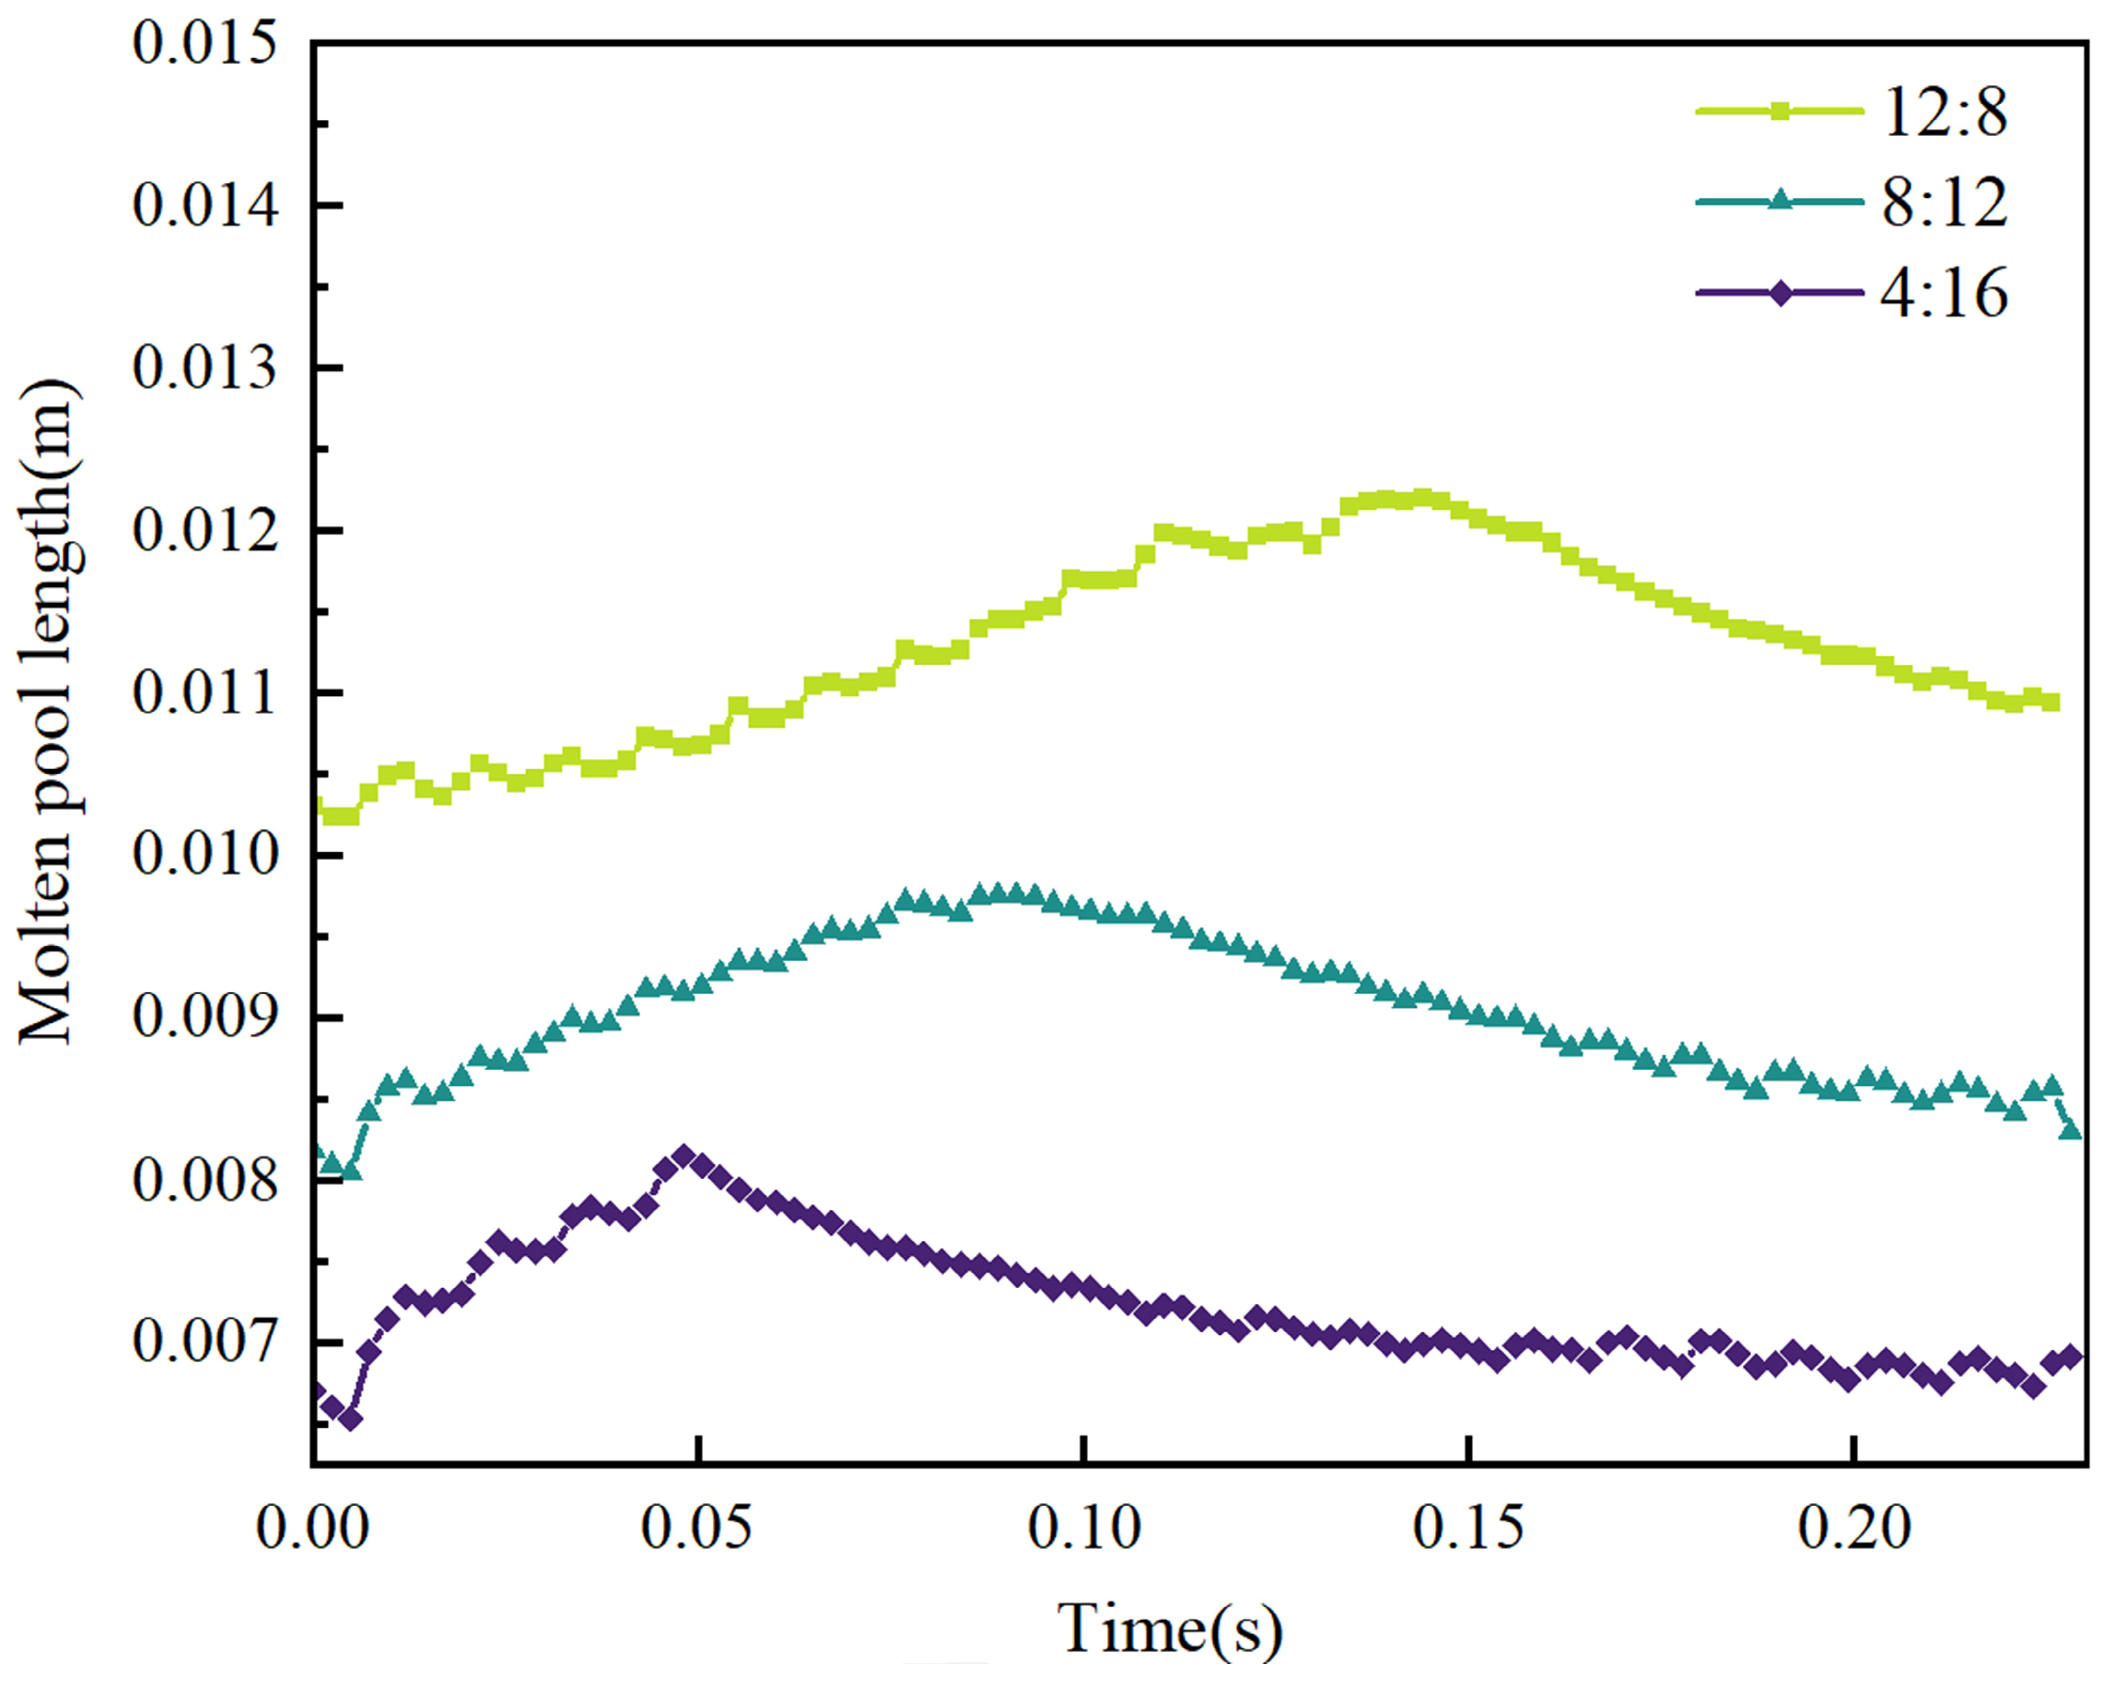
- The molten pool dimensions exhibit periodic dynamic variations, with maximum size positively correlated to the EP proportion. Within a VP-CMT cycle, molten pool length fluctuates cyclically with energy input: high thermal input during the EP phase causes sustained expansion to the cycle’s maximum size; subsequent low thermal input during the EN phase induces cooling, leading to gradual contraction. The thermal accumulation effect is pronounced in multi-layer additive manufacturing, with greater EP proportion resulting in more significant molten pool expansion. Simulations up to the 10th layer showed the maximum molten pool length increasing sequentially with the EP:EN ratio from 4:16, 8:12 to 12:8, reaching 0.0081 m, 0.0098 m and 0.0121 m respectively.
- (3)
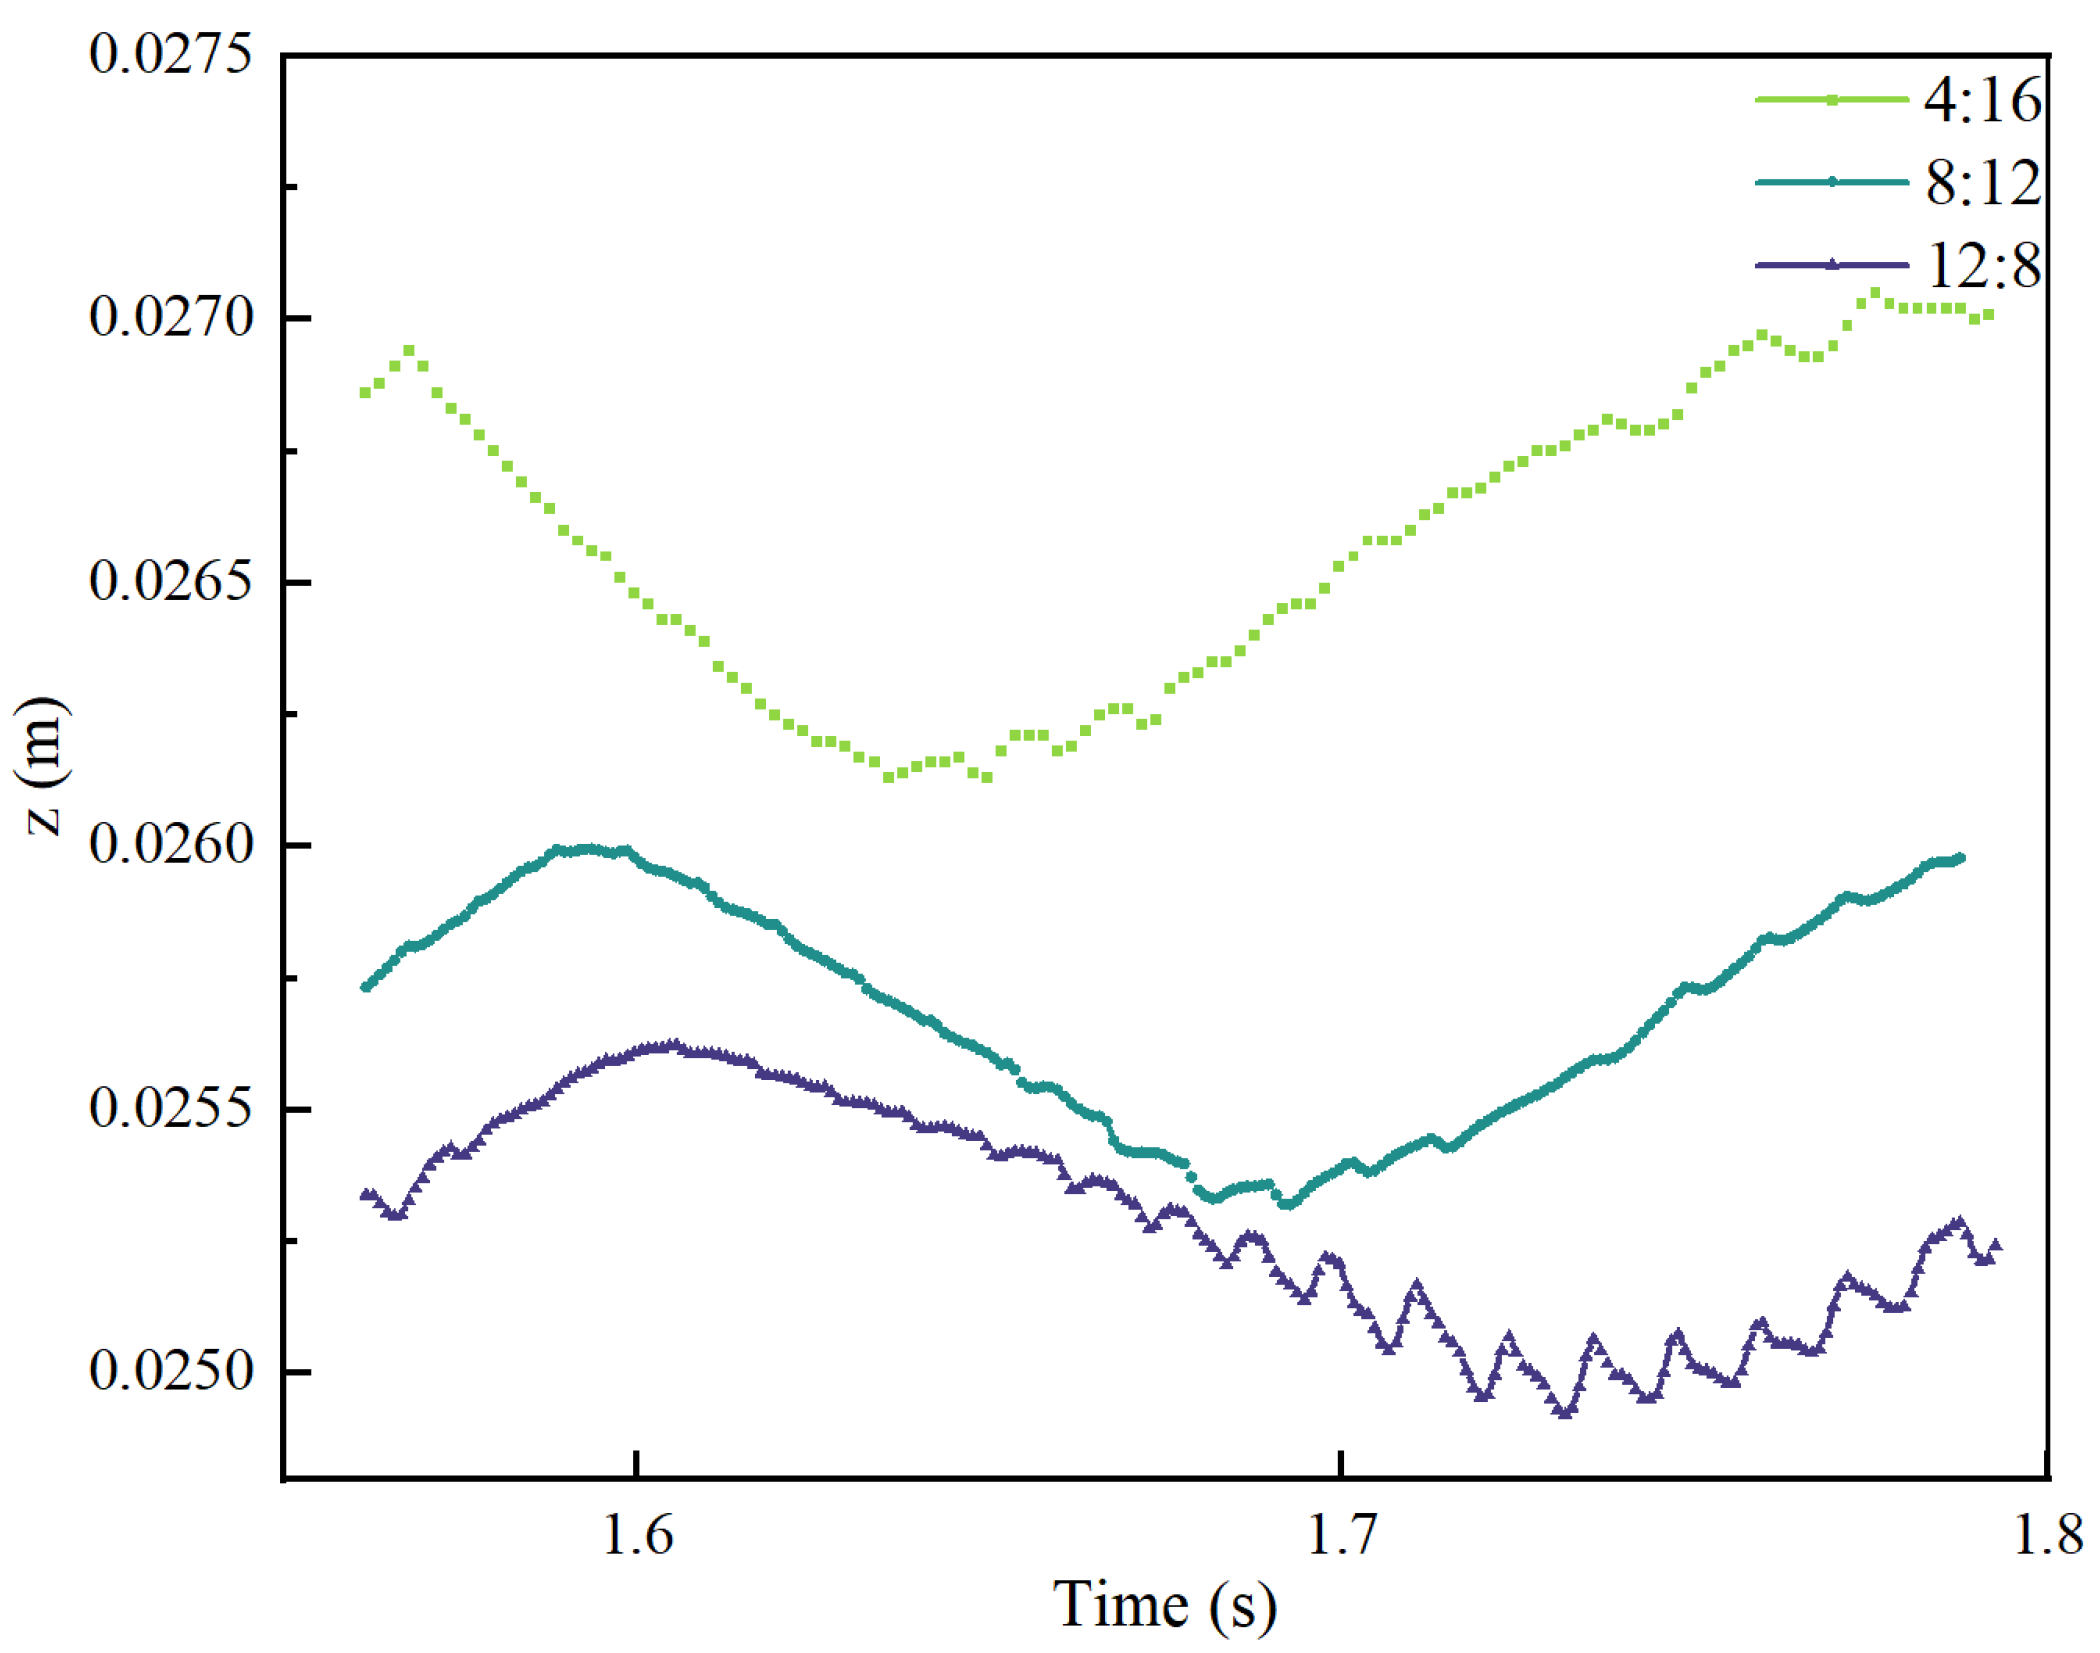
- The degree of melt pool flow intensifies with increasing EP proportion, directly influencing the morphology of the cladding layer. The extent of lateral spread is characterised by the height difference between the surface’s lowest point and the underlying layer. The high thermal input and broad arc pressure range during the EP stage significantly enhance the fluidity and spreading capability of the melt pool metal. Consequently, a higher EP ratio (12:8) results in greater flow, producing a wider and flatter clad layer; conversely, a low EP ratio (4:16) exhibits minimal flow, with the clad layer tending to build upwards and exhibiting reduced width. This provides a basis for controlling the width-to-height ratio of the clad layer by adjusting the EP:EN ratio.
Author Contributions
Funding
Data Availability Statement
Conflicts of Interest
References
- Bao, X.; Yin, H.; Liu, L.; Han, Y. Numerical Simulation of Arc Characteristics of VP-CMT Aluminum Alloy Arc Additive Manu-facturing. Metals 2025, 15, 1360. [Google Scholar] [CrossRef] [Scilit]
- Murphy, A.B.; Tanaka, M.; Yamamoto, K.; Tashiro, S.; Sato, T.; Lowke, J.J. Modelling of thermal plasmas for arc welding: The role of the shielding gas properties and of metal vapour. J. Phys. D Appl. Phys. 2009, 42, 194006. [Google Scholar] [CrossRef] [Scilit]
- Fan, D.; Huang, Z.C.; Huang, J.K. Three-dimensional numerical analysis of the interaction between the arc and weld pool in tungsten inert gas welding considering metal vapour. Acta Phys. Sin. 2015, 64, 304–314. [Google Scholar]
- Wang, X.; Fan, D.; Huang, J.; Huang, Y. Numerical simulation of arc plasma and weld pool in double electrodes tungsten inert gas welding. Int. J. Heat Mass Transf. 2015, 85, 924–934. [Google Scholar] [CrossRef] [Scilit]
- Chen, J.Q.; Xiao, S.H.; Yang, X.Y.; Wu, G. Research progress on numerical simulation heat source models in welding processes. Equip. Manuf. Technol. 2005, 10–14. (In Chinese) [Google Scholar]
- Goldak, J.; Chakravariti, A.; Bibby, M. A new finite element model for welding heat sources. Metall. Trans. B 1984, 15, 299–305. [Google Scholar] [CrossRef] [Scilit]
- Kumar, A.; DebRoy, T. Calculation of three-dimensional electromagnetic force field during arc welding. J. Appl. Phys. 2003, 94, 1267. [Google Scholar] [CrossRef] [Scilit]
- Wu, C. Welding Thermal Processes and Molten Pool Morphology; China Machine Press: Beijing, China, 2008. [Google Scholar]
- Zhou, X.; Zhang, H.; Wang, G.; Bai, X. Three-dimensional numerical simulation of arc and metal transport in arc welding-based additive manufacturing. Int. J. Heat Mass Transf. 2016, 103, 521–537. [Google Scholar] [CrossRef] [Scilit]
- Zhao, W.; Wei, Y.; Long, J.; Chen, J.; Liu, R.; Ou, W. Modelling and simulation of heat transfer, fluid flow and geometry morphology in GMAW-based wire arc additive manufacturing. Weld. World 2021, 65, 1571–1590. [Google Scholar] [CrossRef] [Scilit]
- Ou, W.M. Numerical Simulation and Uniformity Control of MIG Arc Additive Manufacturing Forming. Ph.D. Thesis, Nanjing University of Aeronautics and Astronautics, Nanjing, China, 2020. [Google Scholar]
- Ogino, Y.; Asai, S.; Hirata, Y. Numerical simulation of the WAAM process using a GMAW weld pool model. Weld. World 2018, 62, 393–401. [Google Scholar] [CrossRef] [Scilit]
- Bai, X.; Colegrove, P.; Ding, J.; Zhou, X.; Diao, C.; Bridgeman, P.; Hönnige, J.; Zhang, H.; Williams, S. Numerical analysis of heat transfer and fluid flow in multilayer deposition of PAW-based wire and arc additive manufacturing. Int. J. Heat Mass Transf. 2018, 124, 504–516. [Google Scholar] [CrossRef] [Scilit]
- Lei, Y. Numerical Analysis of Thermal and Fluid Fields in GMA Additive Manufacturing Molten Pool. Master Thesis, Southwest Jiaotong University, Chengdu, China, 2019. [Google Scholar]
- Hashimoto, K.; Hirata, Y.; Kadota, K.; Ogino, Y. Three-dimensional numerical model of short-circuiting transfer in GMAW. Weld. World 2020, 64, 2011–2017. [Google Scholar] [CrossRef] [Scilit]
- Cao, H.; Huang, R.; Yi, H.; Liu, M.; Jia, L. Asymmetric molten pool morphology in wire-arc directed energy deposition: Evolution mechanism and suppression strategy. Addit. Manuf. 2022, 59, 103113. [Google Scholar] [CrossRef] [Scilit]
- Zhao, W.Y.; Cao, X.Y.; Du, X.W.; Wei, Y.H.; Liu, R.P.; Chen, J.C. Numerical simulation of heat and mass transfer in CMT arc additive manufacturing process. Trans. Chin. Soc. Mech. Eng. 2022, 58, 267–276. [Google Scholar]
- He, J.; Ma, R.; Wang, T. Numerical simulation of dynamic behaviour in cold metal transition melt pools during magnesium alloy additive manufacturing. Mater. Sci. Eng. 2022, 30, 18–26. (In Chinese) [Google Scholar]
- Cadiou, S.; Courtois, M.; Carin, M.; Berckmans, W. 3D heat transfer, fluid flow and electromagnetic model for cold metal transfer wire arc additive manufacturing (CMT-WAAM). Addit. Manuf. 2020, 36, 101541. [Google Scholar] [CrossRef] [Scilit]
- Zhao, W.; Tashiro, S.; Murphy, A.B.; Tanaka, M.; Liu, X.; Wei, Y. Deepening the understanding of arc characteristics and metal properties in GMAW-based WAAM with wire retraction via a multi-physics model. J. Manuf. Process. 2023, 97, 260–274. [Google Scholar] [CrossRef] [Scilit]
- Zhou, S.; Xie, H.; Ni, J.; Yang, G.; Qin, L.; Guo, X. Metal transfer behaviour during CMT-based wire arc additive manufacturing of Ti-6Al-4V alloy. J. Manuf. Process. 2022, 82, 159–173. [Google Scholar] [CrossRef] [Scilit]
- Gao, X. Numerical Analysis of Heat Transfer Process and Molten Pool Flow Field in Oscillating Laser-GMAW Hybrid Welding of Lap Joints. Ph.D Thesis, Shandong University, Jinan, China, 2019. [Google Scholar]



| Grade | Mg | Si | Fe | Mn | Cu | Zn | Cr | Ti | Al |
|---|---|---|---|---|---|---|---|---|---|
| ER5356 | 5.1 | 0.04 | 0.09 | 0.15 | 0.01 | 0.01 | 0.07 | 0.08 | Allowance |
| Grade | Mg | Si | Fe | Mn | Cu | Zn | Cr | Ti | Al |
|---|---|---|---|---|---|---|---|---|---|
| 6061 | 1.0 | 0.6 | 0.5 | 0.11 | 0.24 | 0.1 | 0.1 | 0.035 | Allowance |
| Wire Feed Speed (m/min) | Travel Speed (mm/s) | Forward–Reverse Polarity Ratio (EP:EN) |
|---|---|---|
| 4.5 | 8 | 4:16 |
| 4.5 | 8 | 8:12 |
| 4.5 | 8 | 12:8 |
| Wire Feed Speed (m/min) | Movement Speed (mm/s) | EP:EN | Heat Input (J/mm) |
|---|---|---|---|
| 4.5 | 8 | 4:16 | 74.36 |
| 4.5 | 8 | 8:12 | 92.51 |
| 4.5 | 8 | 12:8 | 107.98 |
Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.
Share and Cite
Bao, X.; Han, Y.; Han, F.; Liu, L. Study of Molten Pool Evolution in VP-CMT Aluminium Alloy Arc Additive Manufacturing Under Different EP:EN Ratios. Materials 2026, 19, 1237. https://doi.org/10.3390/ma19061237
Bao X, Han Y, Han F, Liu L. Study of Molten Pool Evolution in VP-CMT Aluminium Alloy Arc Additive Manufacturing Under Different EP:EN Ratios. Materials. 2026; 19(6):1237. https://doi.org/10.3390/ma19061237
Chicago/Turabian StyleBao, Xulei, Yongquan Han, Fubiao Han, and Lele Liu. 2026. "Study of Molten Pool Evolution in VP-CMT Aluminium Alloy Arc Additive Manufacturing Under Different EP:EN Ratios" Materials 19, no. 6: 1237. https://doi.org/10.3390/ma19061237
APA StyleBao, X., Han, Y., Han, F., & Liu, L. (2026). Study of Molten Pool Evolution in VP-CMT Aluminium Alloy Arc Additive Manufacturing Under Different EP:EN Ratios. Materials, 19(6), 1237. https://doi.org/10.3390/ma19061237