


Abstract
In this study, formation water sample No. 1082 from the Narimanov OGPD, together with crude oil samples from the Bulla-Deniz and Muradkhanli fields, was examined under laboratory conditions to evaluate the efficiency of chemical reagents. The Alkan-318 demulsifier, Marza-1 inhibitor, Difron-4201 depressor additive, and a combined ADM composition (Alkan-318 + Difron-4201 + Marza-1 in a 1:1:1 ratio) were tested for their effects on water separation, corrosion inhibition, sulfate-reducing bacterium activity, paraffin deposition, and pour point depression. Comparative experiments showed that the ADM composition demonstrated superior performance over individual reagents at equal concentrations. At an optimal dosage of 600 g/t, the ADM composition reduced the residual water content (mass fraction) of Bulla-Deniz (75% initial water cut) and Muradkhanli (41% initial water cut) crude oils to 0.1 wt.% and 0.8 wt.%, respectively, after thermochemical treatment. The depressant performance was evaluated based on the degree of pour point reduction (ΔT, °C) relative to untreated oil. At optimal concentrations, Difron-4201 and the ADM composition reduced the pour point by 9.0–10.0 °C, demonstrating the superior efficiency of the multifunctional composition compared to individual additives. Corrosion tests revealed that Marza-1 and ADM provided up to 99.9% protection in aggressive H2S and CO2 environments, while ADM also exhibited a nearly complete bactericidal effect (99.8%) against sulfate-reducing bacteria, highlighting its multifunctional efficiency.
1. Introduction
In Azerbaijan, crude oils produced both offshore and onshore differ greatly not only in their physicochemical properties but also in their rheological characteristics. The oils from the developed fields are mostly characterized by common features such as high viscosity and the presence of asphaltene, resin, and paraffin compounds. In many of Azerbaijan’s oilfields, crude oils contain varying amounts of asphaltenes, resins, and paraffins. During the production and transportation of such oils, the deposition of these compounds occurs in the bottomhole zone and in pipelines. To prevent and eliminate these issues, numerous scientific research studies have been conducted by various researchers over time. The complications arising during the extraction, storage, and transportation of water-cut paraffinic oils negatively affect well performance and normal operation, leading to the need for additional downhole and surface repair works.
The complications caused by asphaltene–resin–paraffin deposits (ARPDs) in the well–gathering–transport system, as well as the difficulties encountered in preventing them, are closely related to their specific rheological, structural–mechanical, chemical, and colloid–chemical properties. These difficulties are further aggravated by the wide range of compositions and properties of such deposits. Practically, these deposits are insoluble and consist mainly of organic compounds that tend to disintegrate under crude oil production and transportation conditions.
Reservoir oils and produced crude oils differ primarily in their densities and other quality indicators. When crude oils prepared for transportation enter further refining stages, strict quality requirements are imposed. These include the content of water, sulfur, chlorides, mechanical impurities, and paraffin. Although numerous empirical and semi-empirical models have been proposed to describe crude oil dehydration, paraffin deposition, and corrosion processes, their predictive accuracy remains limited for highly paraffinic, high-water-cut oils due to compositional variability, multiphase flow effects, and dynamic physicochemical interactions. Recent studies have highlighted the challenges in reliably forecasting dehydration efficiency, wax deposition, and corrosion behavior under changing field conditions using existing mathematical models [1,2,3]. On the other hand, during in-field gathering processes, the well products undergo continuous changes not only in rheological and physicochemical characteristics but also in commercial quality. Therefore, during transportation, the selection of unsubstantiated calculation methods and mathematical models without considering both the structural and commercial properties of crude oils with different water cut levels may lead to various complications and increased energy consumption [4,5,6,7].
One of the most important stages of the oil production process is the preparation of crude oil for transportation. Among the main factors that cause complications and additional financial expenses during oil gathering and preparation for transportation are the water cut factor, the deposition of asphaltene–resin–paraffin compounds, and internal surface corrosion processes. The presence of water in oil acts as a ballast, leading to additional transportation costs.
The degree of water dispersion in oil—in other words, water emulsification in crude oil—is one of the key characteristics of oil–water emulsions and determines the essential properties of crude oil. Based on the above considerations, studies were conducted under laboratory conditions to determine the water cut degrees of crude oils using the “drop test” method and the results were analyzed. The drop test method, while originally developed for refined fuels, has also been successfully applied to crude oil–water emulsions for the qualitative and semi-quantitative assessment of emulsion stability and dehydration behavior, particularly in comparative laboratory studies. In the present work, the drop test was used as a screening tool, while quantitative residual water determination was performed using the Dean–Stark distillation method in accordance with ASTM D95—Standard Test Method for Water in Petroleum Products and Bituminous Materials by Distillation [8,9,10].
In global practice, depending on the characteristics of oil emulsions, various methods are applied for their demulsification. Thermochemical demulsification is used to dehydrate emulsions that are difficult to break. During the process, along with heating, different reagents are also applied. Demulsification should be carried out with minimum demulsifier consumption while achieving the maximum dehydration and minimum residual water content.
To eliminate and prevent complications observed in pipelines and on the internal surfaces of technological equipment in oil gathering and transportation systems with highly paraffinic crude oils characterized by a high pour point and high water cut, the optimal approach is the use of chemical reagents [11,12,13,14,15,16].
The electrochemical corrosion of internal surfaces and the formation of asphaltene–resin–paraffin deposits are among the major problems for oilfield equipment. The causes of electrochemical corrosion include the presence of oxygen, hydrogen sulfide, carbon dioxide, sulfate-reducing bacteria in formation waters, and dissolved mineral salts and the precipitation of asphaltene–resin–paraffin compounds. Therefore, the prevention of ARPD formation and the protection of internal surfaces from corrosion are highly relevant issues. The damage caused by these problems to national economies amounts to billions of dollars.
Along with economic losses, environmental damage is also inevitable. The aim of this work was to investigate, under laboratory conditions, the effects of a new multifunctional composition on asphaltene–resin–paraffin deposits, the water cut factor, and corrosion [17,18,19,20].
2. Materials and Methods
To conduct the research process under laboratory conditions, crude oil samples with 75% water cut from well No. 89 of the Bulla-Deniz field and with 41% water cut from the Muradkhanli field, as well as formation water sample No. 1082 from the Narimanov OGPD, were used. Their physicochemical properties are presented in Table 1 and Table 2. Sulfur content was included due to its known influence on electrochemical corrosion processes in oilfield systems.
Table 1.
Physicochemical properties of crude oils.
Table 2.
Ionic composition of formation water from well No. 1082.
The physicochemical properties of the crude oils were determined in accordance with relevant GOST standards. Publicly available descriptions of these methods can be found through the Interstate Council for Standardization, Metrology and Certification (EASC) and national standards repositories.
To ensure consistency, all compositional values in Table 1 are reported using uniform numerical precision (two decimal places). Minor variations in rounding reflect measurement uncertainty inherent to the applied analytical methods.
As shown in the table, the selected crude oil sample for the study belongs to the group of highly paraffinic oils. It is characterized by high content of paraffinic hydrocarbons, a high pour point, and water content of 75% and 41%, respectively.
To date, the widely used “Alkan-318” reagent–demulsifier, applied for crude oil dehydration throughout the country, has demonstrated satisfactory results in tests. Research has shown that this demulsifier can exert a complex effect during oil preparation and transportation processes.
The scientific justification for using the “Alkan-318” reagent–demulsifier has been established—namely, to regulate the flow and processing characteristics of oils with complex rheological properties, as well as to ensure efficient preparation and transportation.
For the studied crude oil sample, the effects of both the “Alkan-318” demulsifier and the ADM composition—prepared from the “Alkan-318” demulsifier, “Difron-4201” additive, and Marza-1 inhibitor in a 1:1:1 ratio—were investigated.
The laboratory dehydration of the studied oil was performed using the efficient “Boatels Test” (“Bottle Test”) method, both without reagents and with the reagent or composition. Experiments were conducted based on the emulsion breakage time. The demulsification time was determined by measuring the volume of settled water in the bottle, and, after the separation process was complete, the residual water content in the oil was determined using a balance method.
The “Alkan-318” reagent–demulsifier, which showed high efficiency in crude oil emulsion dehydration, was used in the experiments. To carry out the tests, crude oil samples with varying water cut levels were dosed with the reagent and composition at established consumption rates, and then control samples were taken. During the experiments, temperature stability (20 °C, 40 °C, and 60 °C) was maintained, and multiple studies were performed.
The efficiency of emulsion separation by the demulsifier was evaluated using the “Bottle Test” method. Assessment was based on the amount of water separated from the stable oil–water system over time. The amount of water present in the crude oil was determined using the Dina–Stark method. To accurately measure the water separated during demulsification, a specialized glass separator with a defined volume was used.
In this study, the residual water content was determined by the Dina–Stark distillation method, while the amount of separated water during demulsification was used to evaluate the kinetics of phase separation. Formula (1) therefore describes the relative efficiency of water separation, whereas the final residual water content values reported in the tables correspond to gravimetrically confirmed distillation results.
Here, m0 is the amount of water before demulsification, g.
m is the amount of water separated during demulsification, g.
Table 3 presents the physicochemical properties of the “Alkan-318” demulsifier.
Table 3.
Physicochemical properties of the “Alkan-318” demulsifier.
Given the high paraffinicity of the studied oil, the process of asphalt–resin–paraffin deposit (ARPD) formation in its composition was determined under laboratory conditions using both the “Difron-4201” additive and the ADM composition. This was carried out at 50 °C over a 3 h period via the “cold finger” method.
The core principle of the method involves the deposition of asphalt–resin–paraffin compounds on the surface of a cold metal probe (“cold finger”). This enables the evaluation of the effectiveness of both the depressant additive and the composition, as well as the determination of the optimal dosage.
The physicochemical indicators of the Difron-4201 depressant additive are presented in Table 4.
Table 4.
Physicochemical indicators of the “Difron-4201” depressant additive.
During the research, the effectiveness of the “Difron-4201” depressant additive and the ADM composition was calculated using a given formula. This was done after determining the quantity of deposits formed on the cold metal surface for both oil samples, which had been treated with various concentrations of the additives, by means of the gravimetric method.
K—effectiveness of the depressant additive;
m1—mass of the asphalt–resin–paraffin deposits (ARPDs) in the additive-free medium;
m2—mass of the ARPDs in the medium containing the depressant additive and composition.
The mass of asphaltene–resin–paraffin deposits (m1 and m2) was determined gravimetrically after deposition on the cold finger surface, followed by mechanical removal, solvent washing to eliminate residual oil, drying to a constant mass, and weighing using an analytical balance.
To determine the effect of the “Difron-4201” depressant additive and the ADM composition on the pour point of oil under laboratory conditions, a known volume of an oil sample was placed into test jars with a spherical bottom, 160 mm in height and 20 mm in diameter, and heated to a temperature of 55–60 °C. The experiment was continued by gradually cooling the test jar to 30–40 °C after adding various concentrations of the depressant additive and composition separately to the oil sample.
After the test jars, cooled to a known temperature, were placed in a thermostat, the cooling process was continued. The temperature at which the oil’s meniscus remained stationary for a minimum of 5 s while the jar was held horizontally at a 45-degree angle was recorded every time the temperature decreased by 1 °C. The complete solidification of the oil was determined based on the immobility of the upper layer of the liquid.
In oil gathering and transportation systems, alongside problems of water cut and paraffin deposition, complications arising from internal surface corrosion, which require urgent solutions, are also a central focus. To eliminate this complication, the corrosion protection effect of the “Marza-1” inhibitor and the ADM composition was determined using a steel sample of grade St20, with dimensions of 30 × 20 × 1 mm. The chemical composition of the St20-grade steel sample is given in Table 5.
Table 5.
Chemical composition of St20-grade steel (%).
The corrosion rate of the steel sample was determined through laboratory experiments under dynamic conditions based on gravimetric tests. To conduct tests under dynamic conditions, a flow rate corresponding to operational conditions was achieved using a circulation apparatus. The corrosion rate was calculated based on the mass loss.
The research was conducted at a temperature of 25 °C over a duration of 6 h, using various concentrations of the Marza-1 inhibitor. Marza-1 is a mixed organic corrosion inhibitor belonging to the class of unsaturated nitrogen- and heteroatom-containing compounds, capable of adsorption on steel surfaces through π-electron systems and heteroatoms, forming a protective barrier against electrochemical corrosion and bacterial activity (Table 6) [30].
Table 6.
Physicochemical characteristics of the “Marza-1” reagent.
The boiling point is reported at reduced pressure (1 mmHg) and is provided for only physicochemical characterization. Corrosion and bactericidal tests were conducted at ambient temperature (25 °C). The experiments were conducted as follows: the surfaces of the steel samples were ground on a grinding machine; subsequently, they were cleaned with acetone and alcohol and then washed with distilled water.
Following this, the surfaces were activated by immersing them in a 15% HCl solution for 60 s, washed again with distilled water, and dried with filter paper. The mass of the sample was determined on an analytical balance after it was stored in a desiccator for one hour.
The experiments were carried out for comparison purposes: without any inhibitor, with the inhibitor, and with the composition.
The corrosion rate was calculated using the following formula:
m1—mass of the steel sample before the test, g;
m2—mass of the steel sample after the test and the removal of corrosion products, g;
S—surface area of the steel plate (SN = 2ah + 2ab + 2bh), m2;
τ—duration of the laboratory test, hours.
The following mathematical expression was used to calculate the inhibition coefficient.
Here, K0—the corrosion rate in an environment without the inhibitor or composition (g/m2·h);
Kinh—the corrosion rate in an environment with the inhibitor or composition (g/m2·h).
The protective effect of the inhibitor and composition was calculated using the given formula:
The penetration depth was determined based on the corrosion rate using the following formula:
Here, Kp—penetration depth, mm/year;
Kinh—corrosion rate, g/m2·h.
The bactericidal properties of the Marza-1 inhibitor and ADM composition against sulfate-reducing bacteria were studied in the “Postgate-B” nutrient medium (Table 7).
Table 7.
Composition of the “Postgate-B” nutrient medium, g/L.
In hydrogen sulfide-containing formation water, the properties of both the inhibitor and the composition were studied under laboratory conditions, and their protective effects against corrosion were determined. As the corrosion medium, formation water samples from well No. 1082 of the Bibiheybatneft OGPD and bacterial strains of Desulfomicrobium and Desulfovibrio desulfuricans were used.
Based on the amount of hydrogen sulfide, the bactericidal effects of the inhibitor and the composition were calculated using the following formula:
Here, C0—concentration of biogenic hydrogen sulfide in the medium without the inhibitor or composition;
Cinh—concentration of biogenic hydrogen sulfide in the medium with the inhibitor or composition reagent.
Experimental Reproducibility and Statistical Analysis
All laboratory experiments were conducted in triplicate under identical conditions to ensure the reproducibility of the results. For each experimental condition, three independent runs were performed, and the reported values represent the arithmetic mean of the measurements. Standard deviations were calculated for key performance indicators, including the residual water content after demulsification, pour point reduction, asphaltene–resin–paraffin deposit (ARPD) inhibition efficiency, corrosion protection efficiency, and bactericidal activity.
The relative standard deviation of repeated measurements did not exceed ±5%, indicating good experimental repeatability and measurement stability. A comparative statistical analysis between individual reagents and the ADM composition was performed using one-way analysis of variance (ANOVA) at a 95% confidence level (p < 0.05). The statistical evaluation confirmed that the improvements achieved by the ADM composition over individual reagents were statistically significant.
3. Results
Under laboratory conditions, the thermochemical demulsification of Bulla-Deniz crude oil with 75% water cut and Muradkhanli crude oil with 41% water cut was carried out in the presence of the reagent and the composition. The demulsification process was performed using the demulsifier and the composition at dosages of 300–600 g/t, at temperatures of 20, 40, and 60 °C, and for various settling times of water (40, 60, 80, 120 min).
Table 8 presents the parameters obtained from the experiments.
Table 8.
Results of the demulsification of Bulla-Deniz crude oil with 75% water cut and Muradkhanli crude oil with 41% water cut.
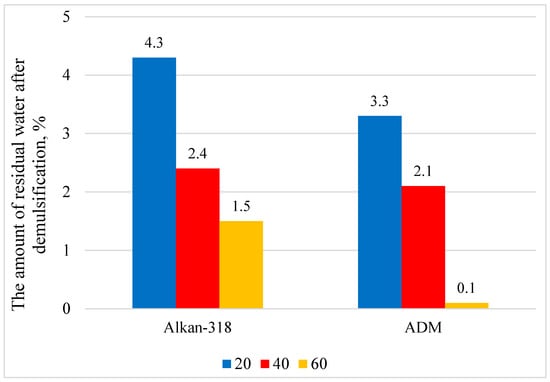
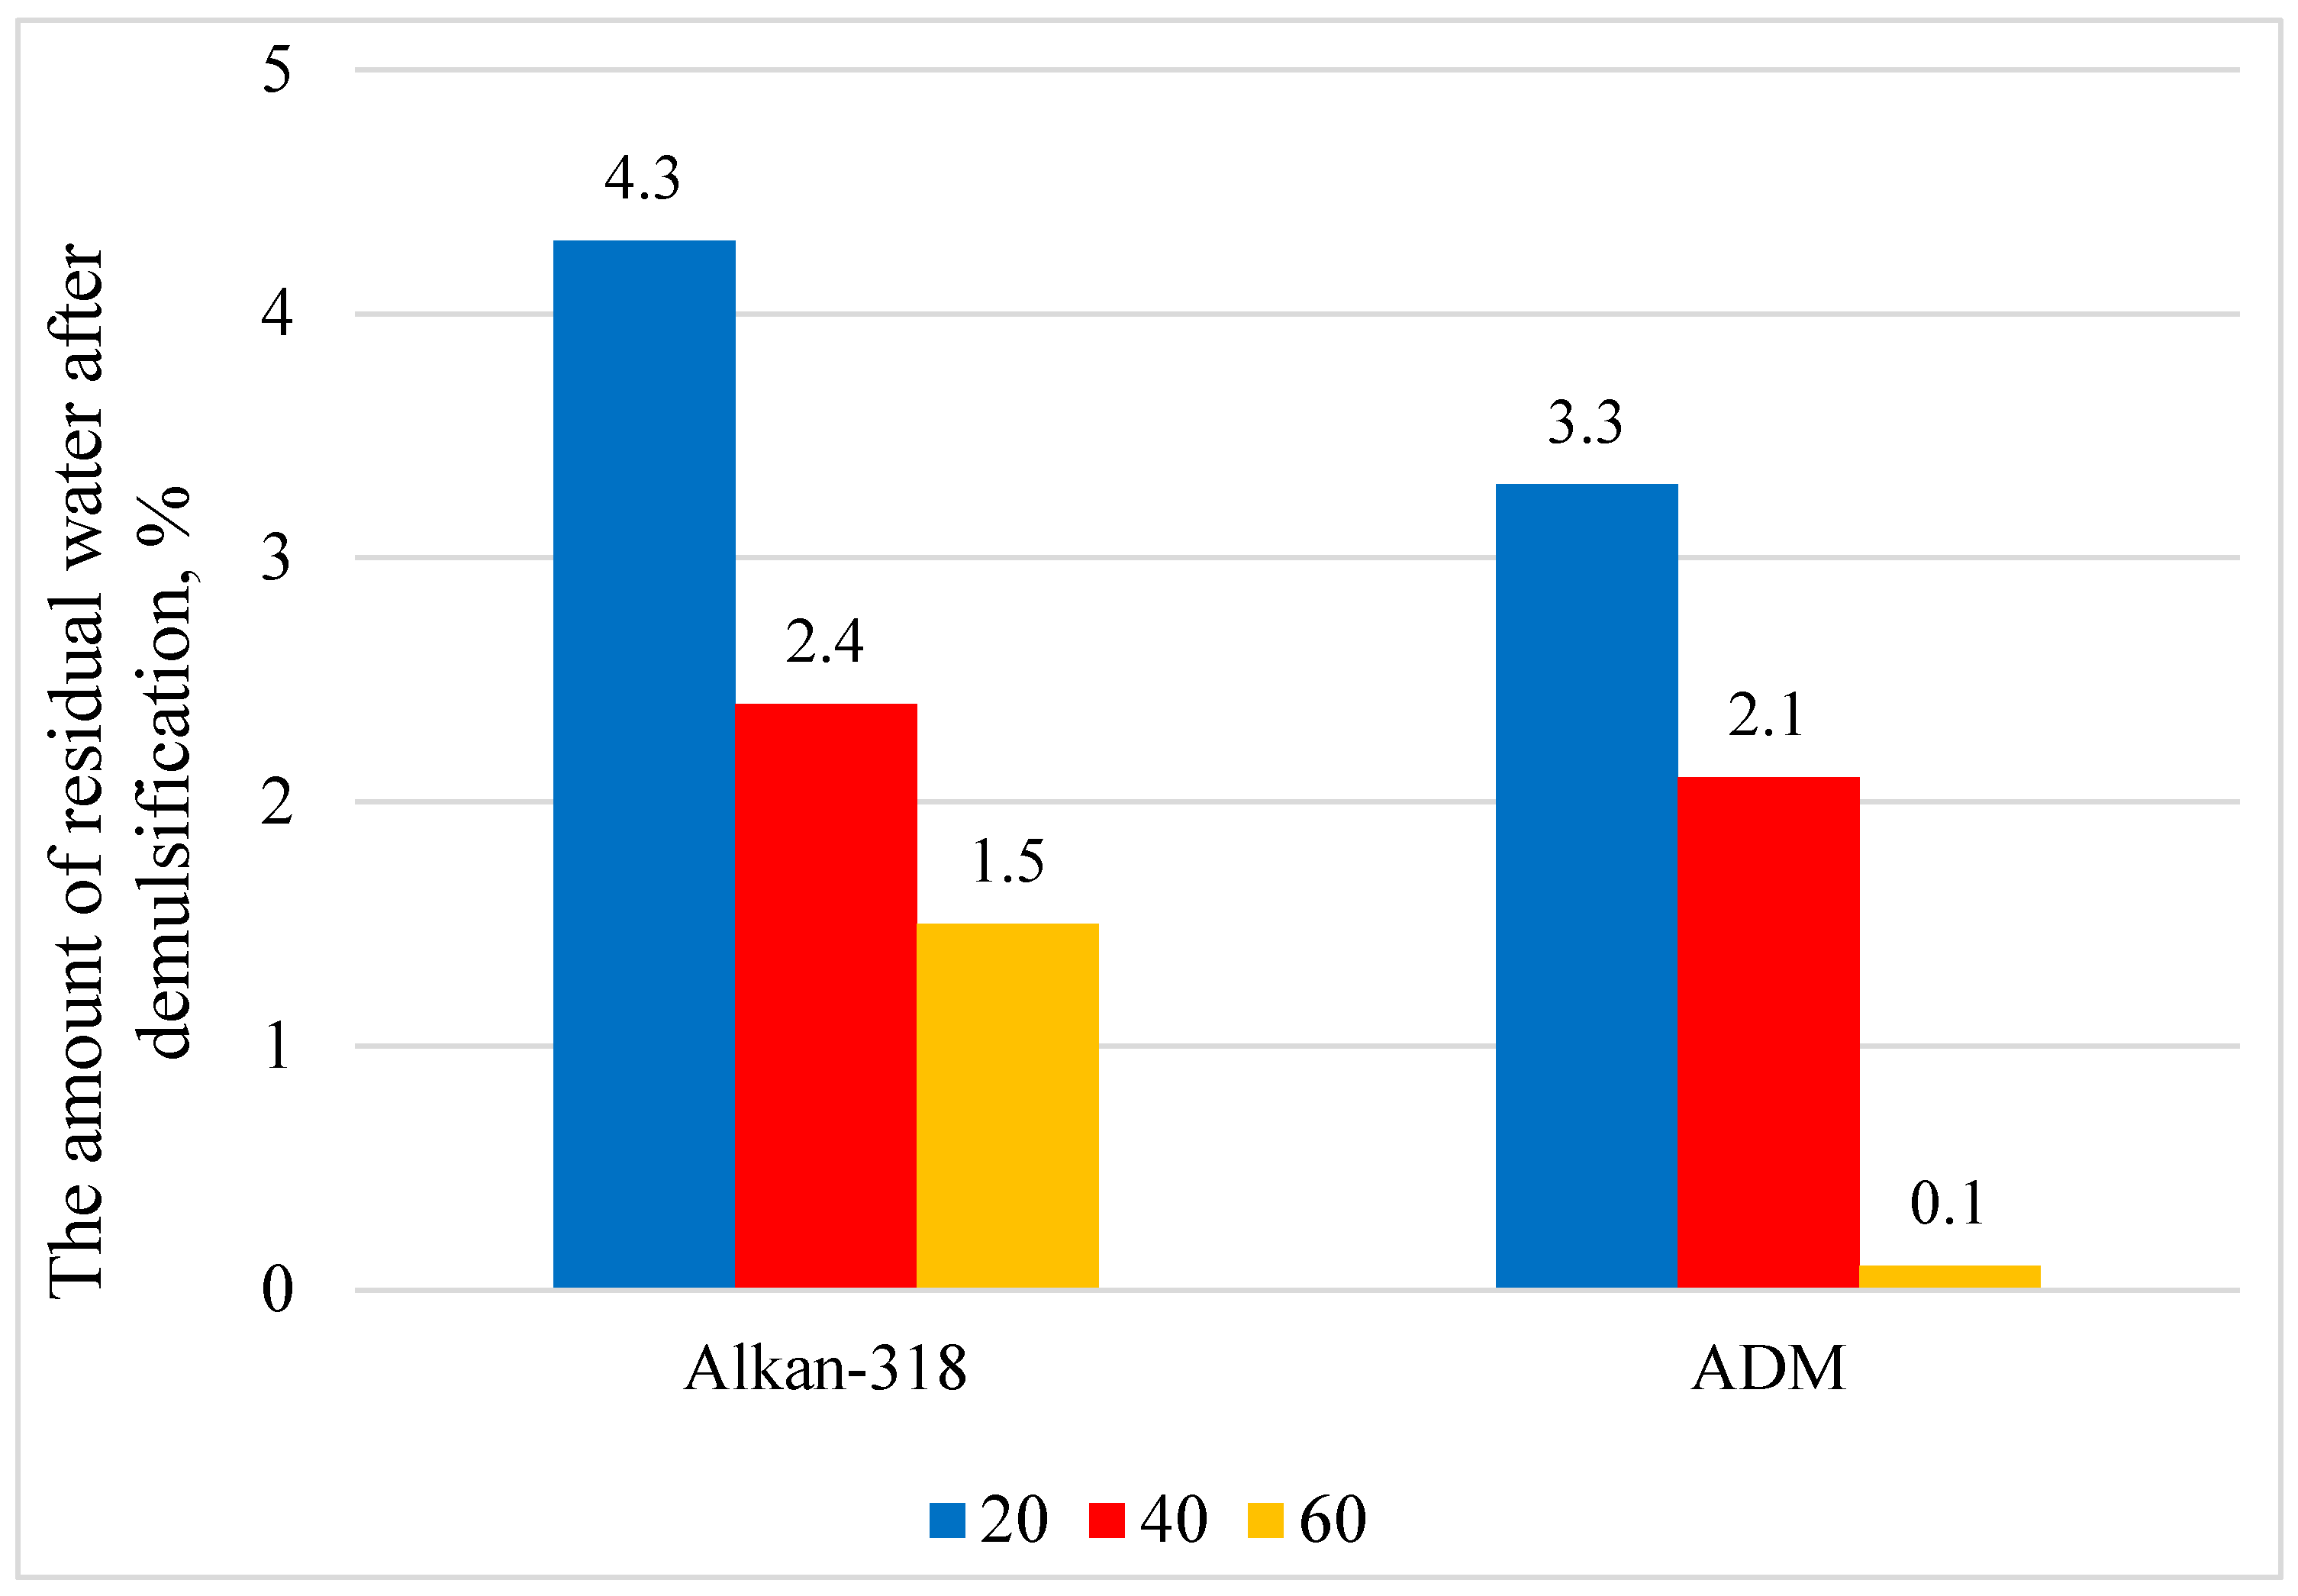
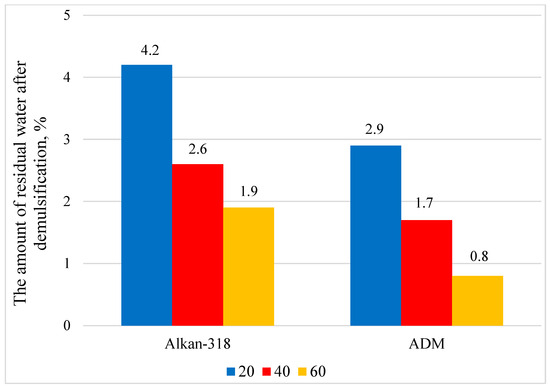
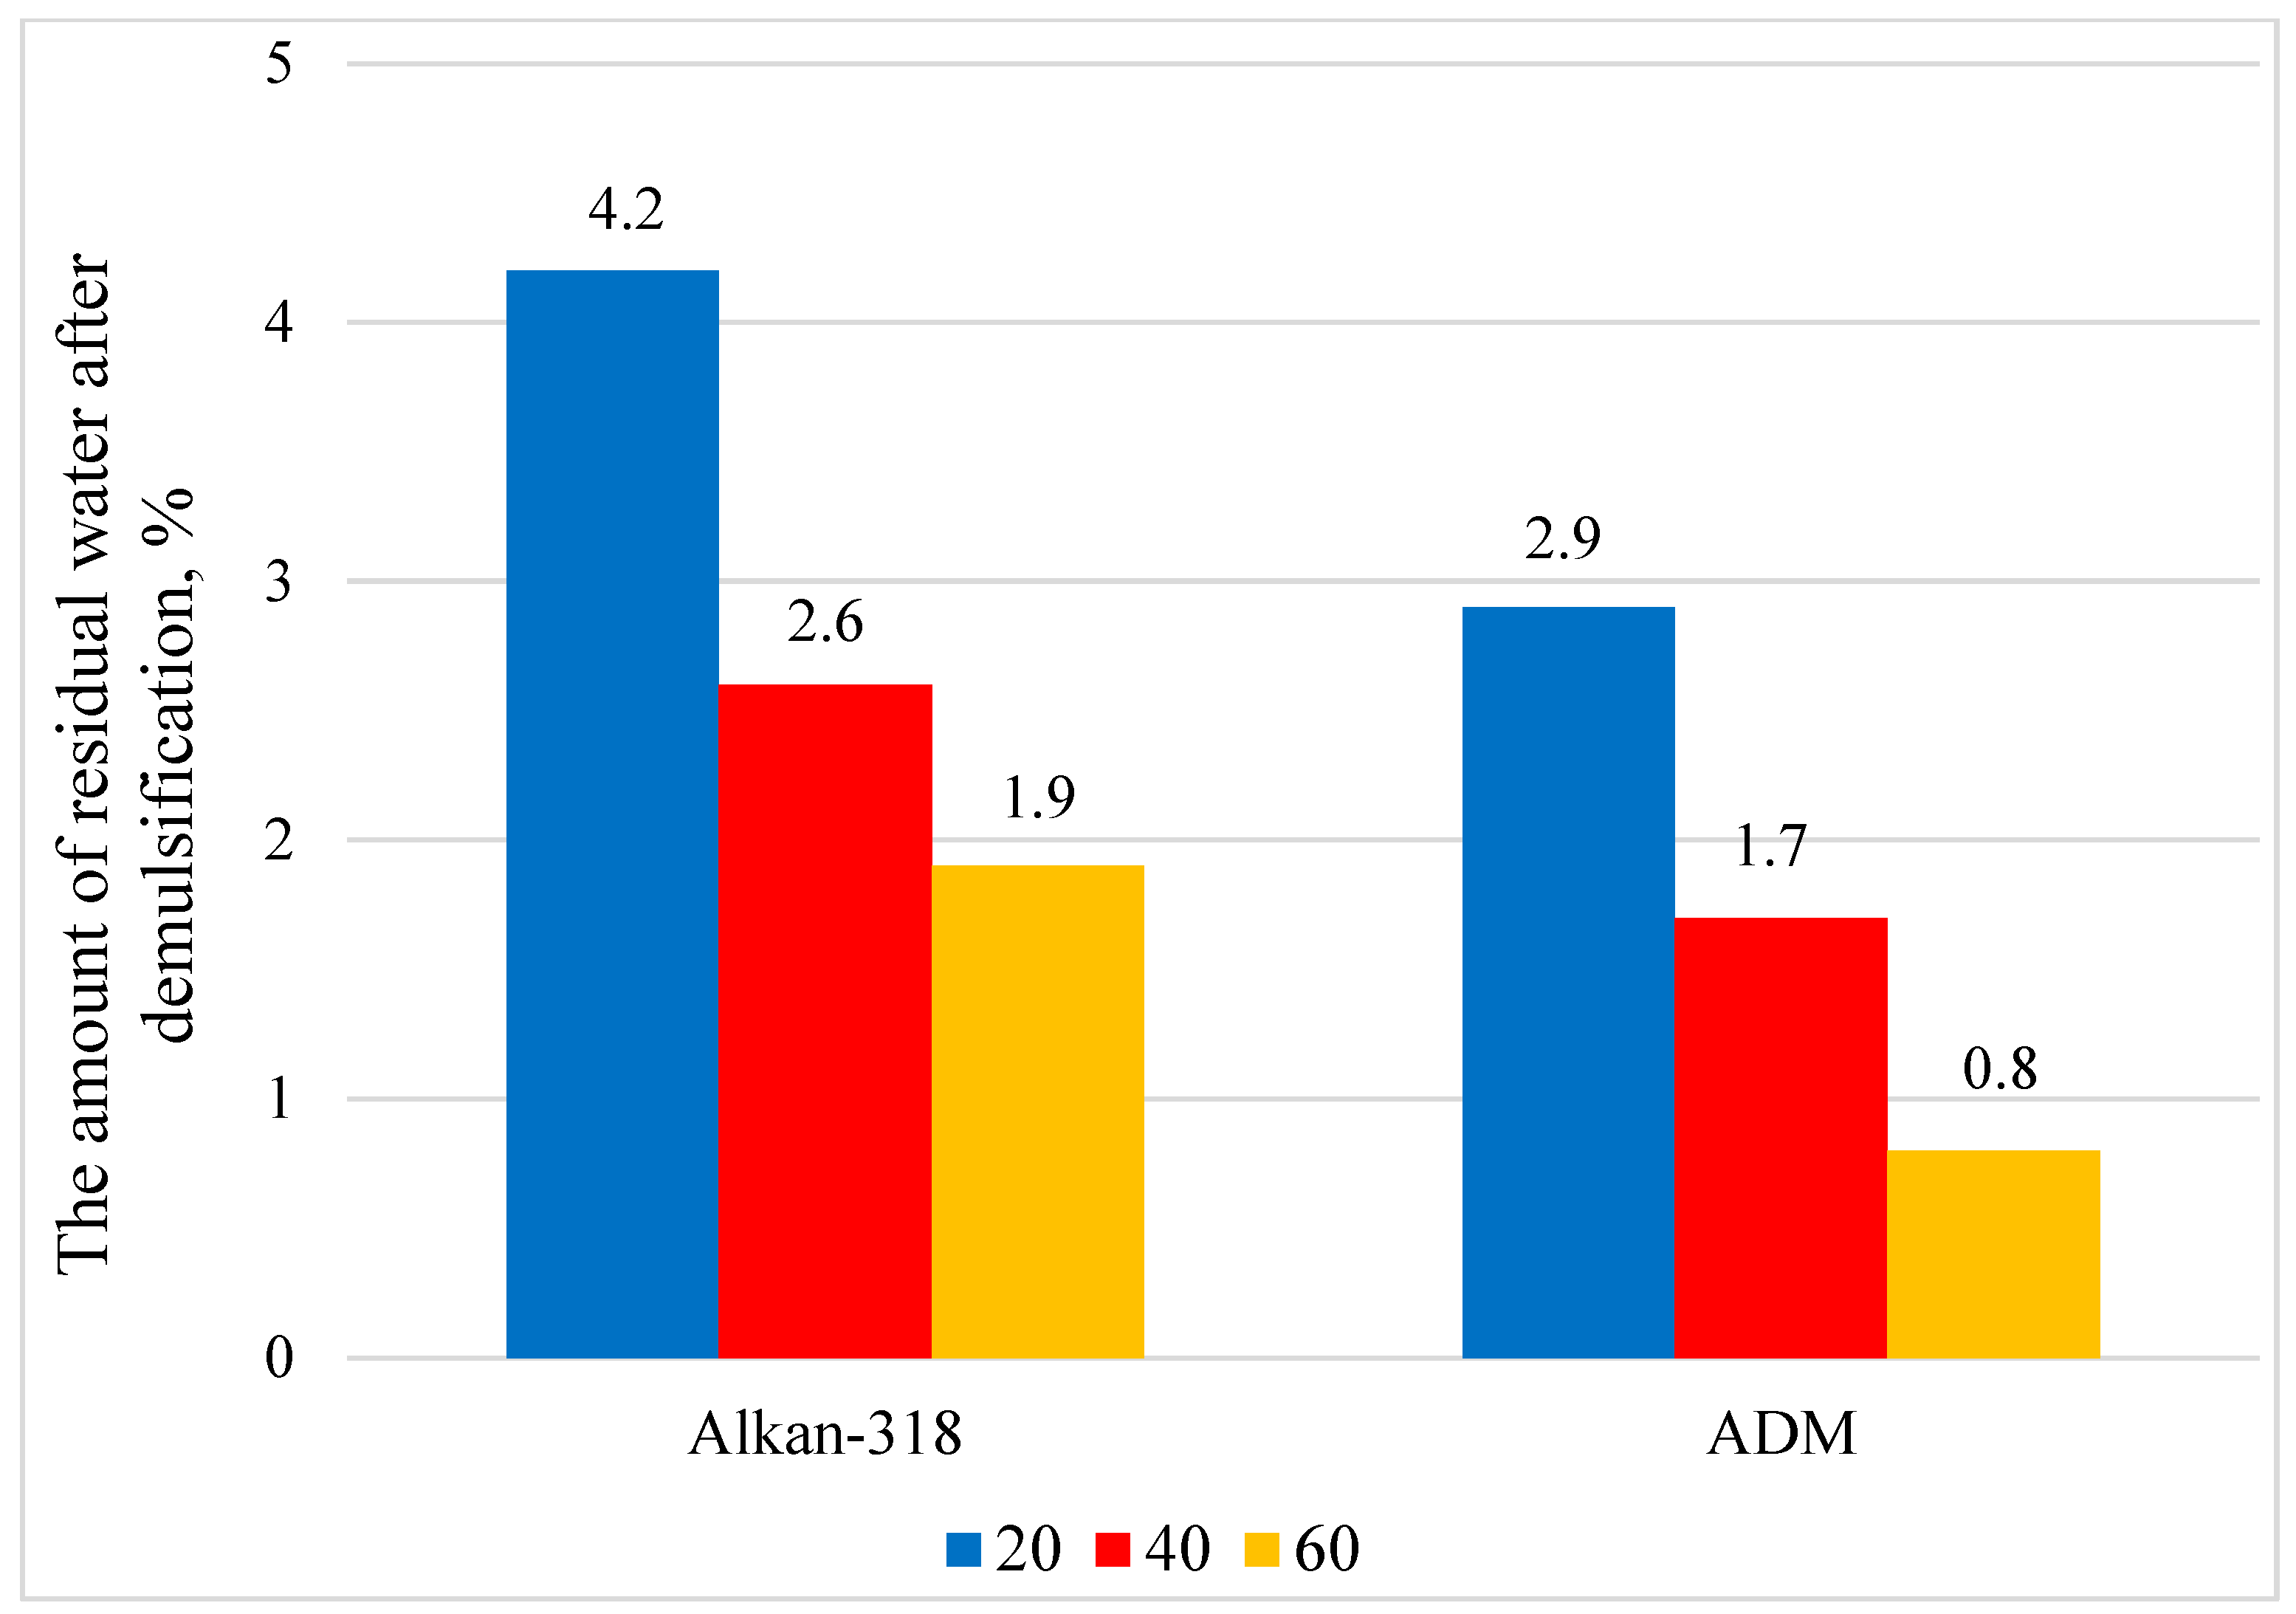
It can be seen from the table that the efficiency of the crude oil emulsions’ demulsification with the reagent and composition at 20 °C and 40 °C was low, while the best results were achieved during the dehydration process conducted at 60 °C. In Table 8, it is shown that, at 60 °C and within the concentration range of 300–600 g/t of the Alkan-318 reagent, the residual water content for the Bulla-Deniz crude oil varied between 5.9% and 1.5%, while, for the Muradkhanli crude oil, it ranged between 5.7% and 1.9%. The non-linear variation in the residual water content observed for the Muradkhanli crude oil without a reagent at different temperatures is attributed to the complex stability of natural emulsions. A temperature increase initially promotes water separation; however, the partial re-dispersion and stabilization of fine water droplets may occur due to the natural surfactants present in the crude oil, resulting in non-monotonic behavior. Similar trends have been reported for untreated water–oil emulsions with high resin and asphaltene content.
The mass of separated water corresponds to the experimentally collected aqueous phase during the demulsification of a fixed-mass crude oil sample with known initial water content. For example, for the Bulla-Deniz oil with 75 wt.% water cut, separation of ~74 g of water from a 100 g emulsion sample is consistent with the residual water values obtained by distillation.
The effect of the ADM composition, obtained by mixing the reagents Alkan-318, Marza-1, and Difron-4201 in a 1:1:1 ratio based on laboratory tests, on the studied oils was investigated. According to the results, as reflected in Table 9, the residual water content for the Bulla-Deniz oil varied between 4.1% and 0.1%, and that for the Muradkhanli oil between 4.3% and 0.8%, within the concentration range of 300–600 g/t at a temperature of 60 °C.
Table 9.
Results of the demulsification of Bulla-Deniz oil with 75% water cut and Muradkhanli oil with 41% water cut.
The comparison of the dependence of the residual water content on the temperature after the demulsification of the 75% water-cut Bulla-Deniz oil and 41% water-cut Muradkhanli oil with the participation of the reagent and composition is given in Figure 1 and Figure 2.
Figure 1.
The dependence of the residual water content in Bulla-Deniz oil on the temperature after demulsification.
Figure 2.
The dependence of the residual water content in Muradkhanli oil on the temperature after demulsification.
The effectiveness of the “Difron-4201” depressant additive and the ADM composition on samples of Bulla-Deniz and Muradkhanli oil was calculated under laboratory conditions based on the amount of collected asphaltene–tar–paraffin deposits using the “cold finger” method. Over a one-hour period at a temperature of 0 °C, the amount of deposits, as well as the oil’s pour point, surface tension coefficient, and effective viscosity, was determined in the presence of both the depressant additive and the composition at quantities of 100–600 g/t. The test results are presented in Table 10.
Table 10.
Effects of the “Difron-4201” depressant additive and the ADM composition (Alkan-318 + Difron-4201 + Marza-1 = 1:1:1) (at +0 °C) on a series of properties of Bulla-Deniz and Muradkhanli oils.
The non-monotonic variation in the ARPD mass observed with increasing concentrations of the ADM composition is associated with competing physicochemical mechanisms. At moderate dosages, crystal growth inhibition dominates, resulting in minimal deposit formation. At higher concentrations, the partial reaggregation of modified paraffin crystals may occur, followed by renewed inhibition as the adsorption equilibrium stabilizes. Such behavior is characteristic of depressant additives acting through surface-active mechanisms. The listed concentrations correspond to separate experiments conducted with either Difron-4201 or the ADM composition and do not represent cumulative mixture concentrations.
The calculated efficiencies of pour point reduction, ARPD inhibition, and surface tension reduction are summarized in Table 11.
Table 11.
The effectiveness of the “Difron-4201” depressant additive and the ADM composition (Alkan-318 + Difron-4201 + Marza-1 = 1:1:1) on a series of properties of Bulla-Deniz and Muradkhanli oils (at t = +0 °C).
Table 11 summarizes the calculated effectiveness of the Difron-4201 depressant additive and the ADM composition in terms of pour point reduction, asphaltene–resin–paraffin deposit (ARPD) inhibition, and surface tension reduction for both crude oils. As shown in the table, the effectiveness of all three parameters increases with increasing concentrations for both systems. For both the Bulla-Deniz and Muradkhanli oils, the ADM composition consistently demonstrates higher effectiveness than the individual depressant additive at comparable concentrations. The maximum performance is observed at a concentration of 600 g/t, where the ADM composition provides the highest combined efficiency in reducing the pour point, suppressing ARPD formation, and lowering surface tension, confirming its synergistic multifunctional behavior.
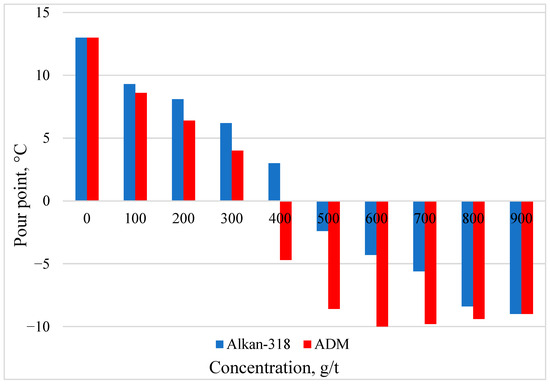
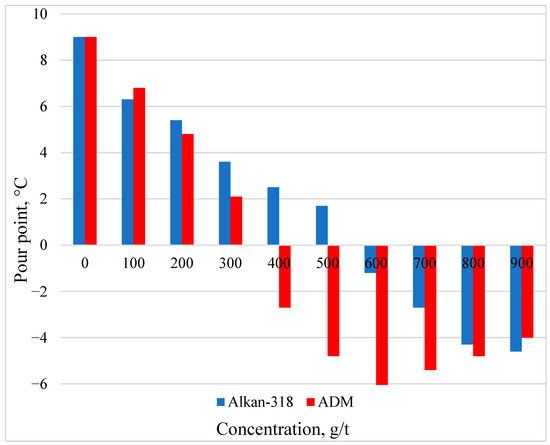
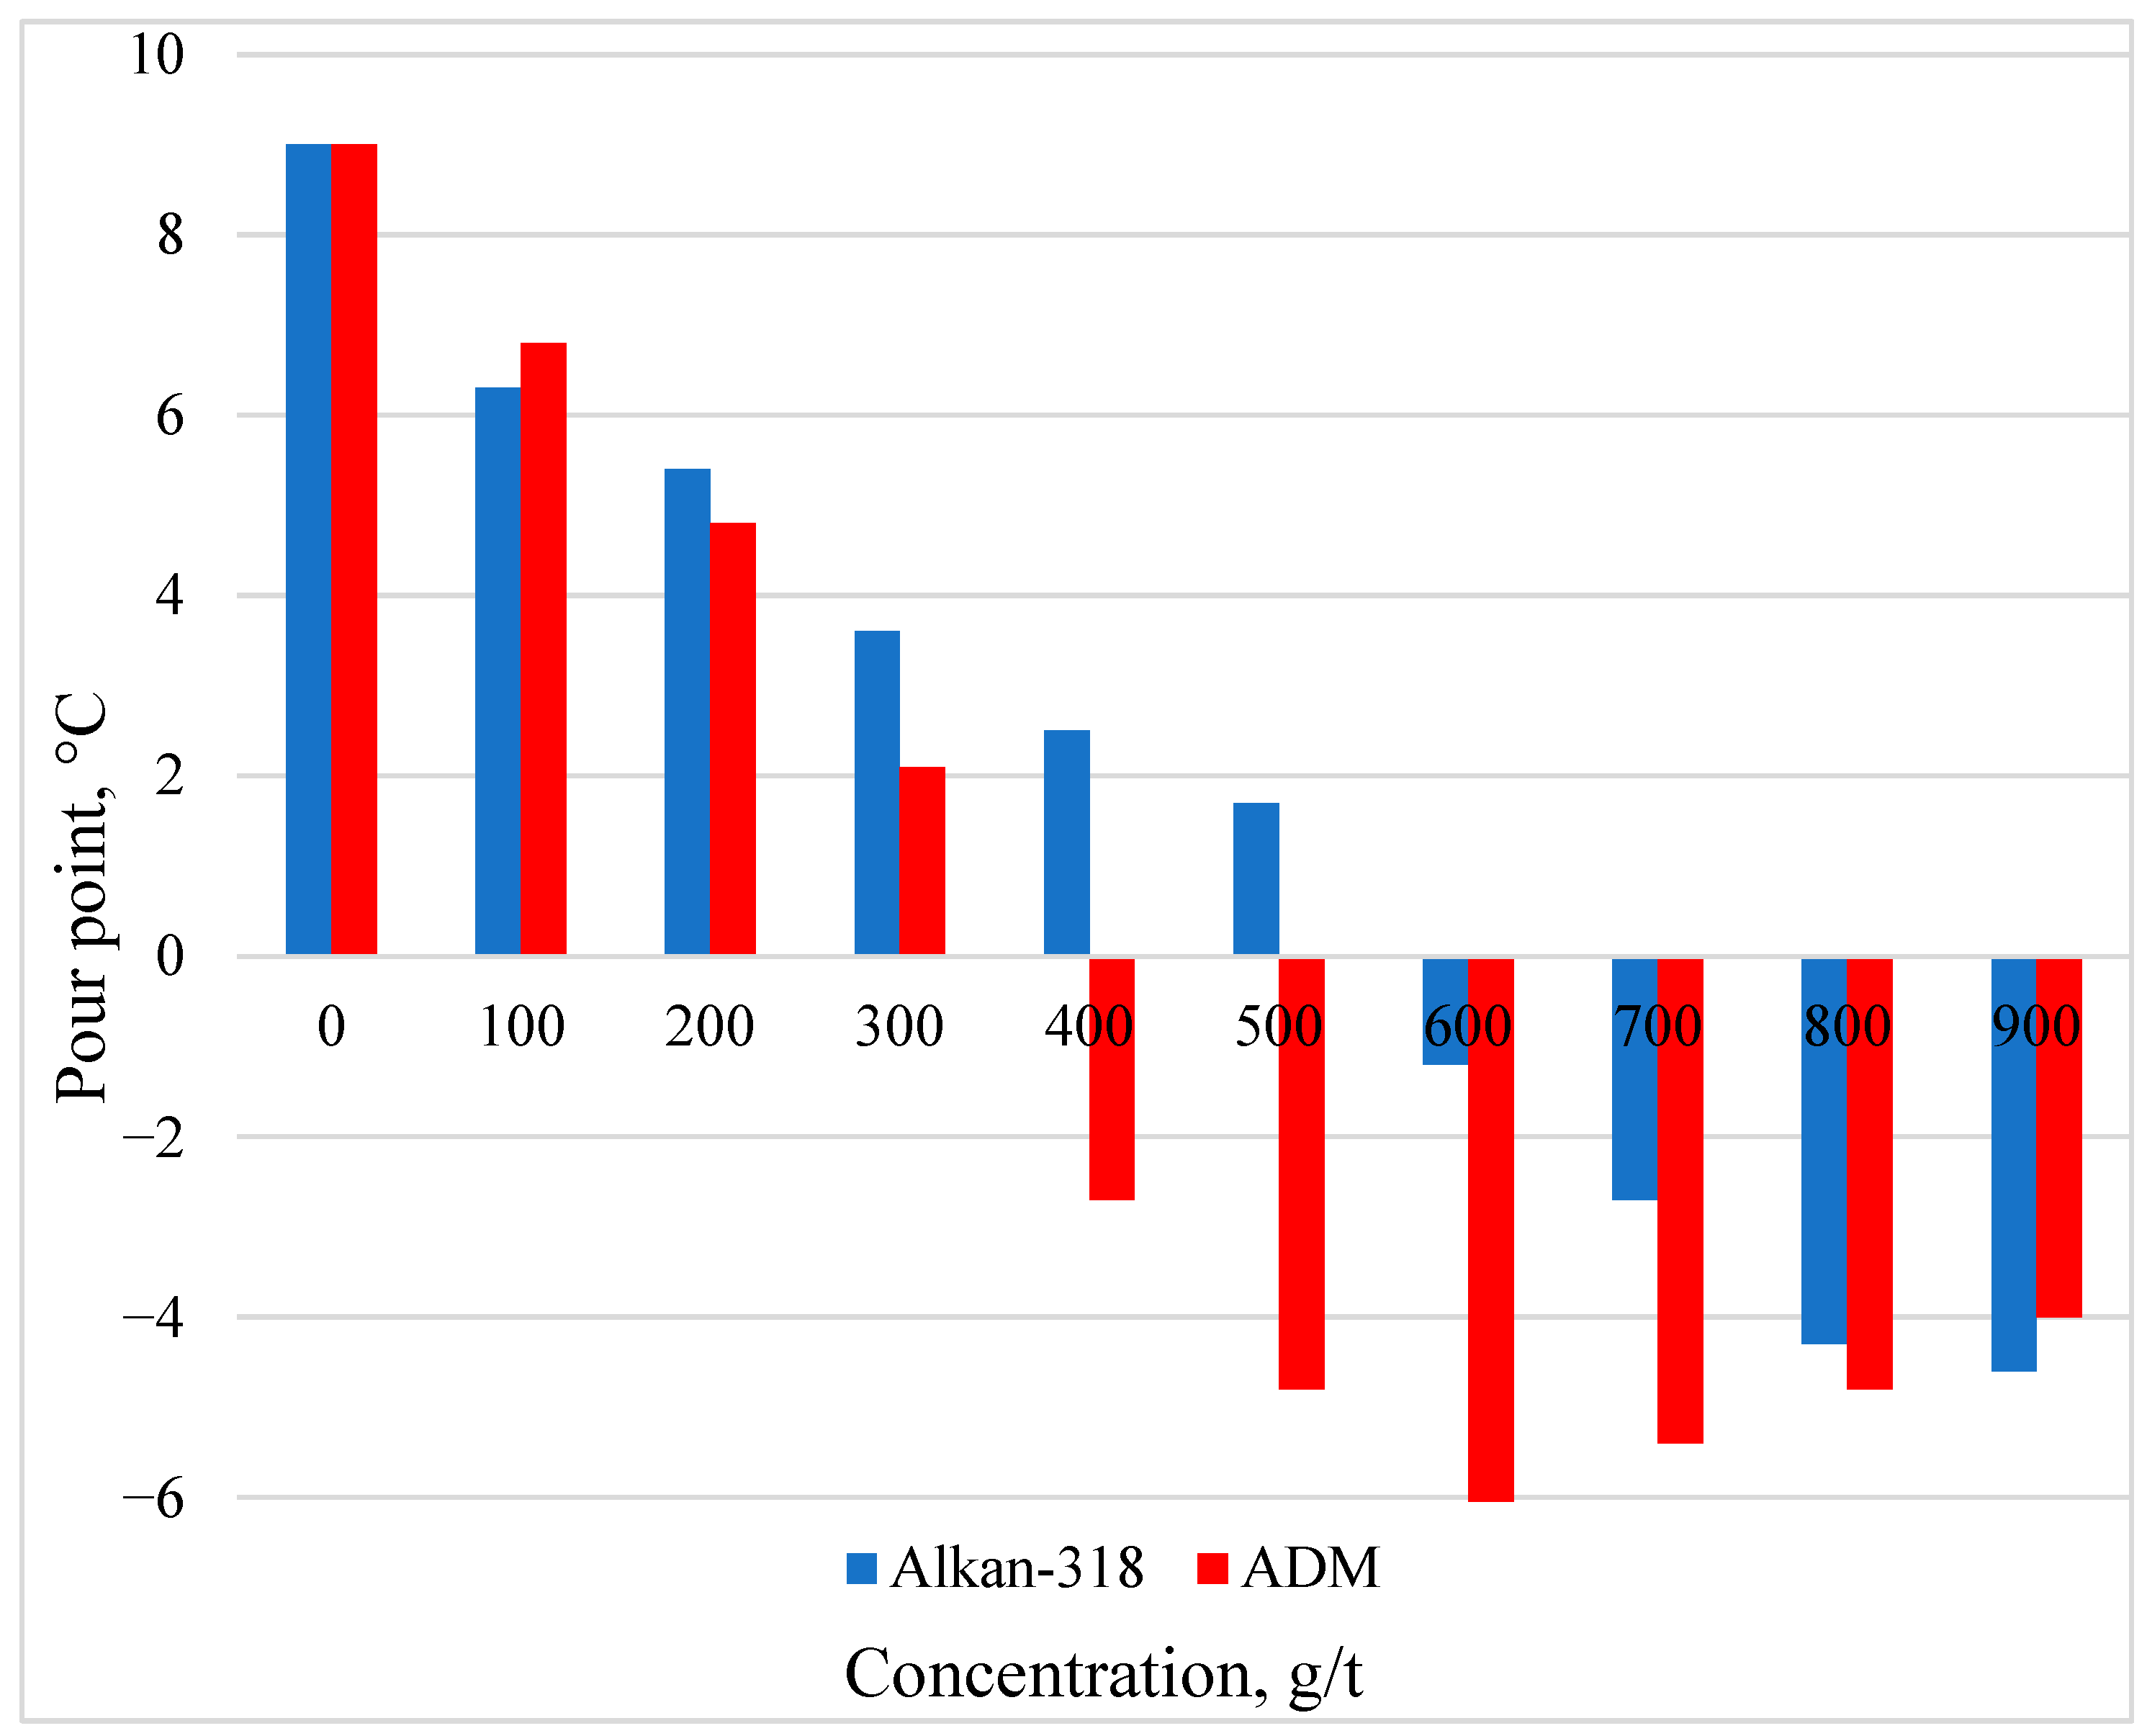
A comparative analysis of the change in the freezing point of the studied Bulla-Deniz and Muradkhanli oils under laboratory conditions, depending on the concentration of the reagent and composition, is reflected in Figure 3 and Figure 4.
Figure 3.
The dependence of the pour point of Bulla-Deniz oil on the concentration.
Figure 4.
The dependence of the pour point of Muradkhanli oil on the concentration.
Therefore, the effect of the “Difron-4201” depressant additive and the ADM composition on the pour point, paraffin deposition, and surface tension of Bulla-Deniz and Muradkhanli oil samples was investigated for the first time. It was determined that the composition demonstrated higher effectiveness.
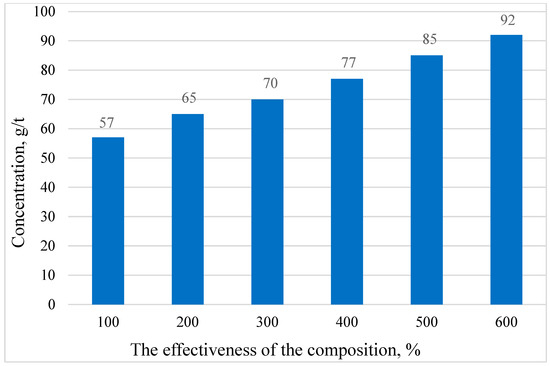
The highest effectiveness was observed at an optimal dosage of 600 g/t for both the “Difron-4201” depressant additive and the ADM composition (Figure 5).
Figure 5.
The effectiveness of the ADM composition at various concentrations.
Specifically, at this concentration, the highest effectiveness in reducing the pour point was 169.2% for the Bulla-Deniz oil and 151.4% for the Muradkhanli oil when using the “Difron-4201” depressant additive. For the ADM composition, the highest effectiveness was 176.9% and 170.0% for the respective oils.
The protective effectiveness against asphaltene–resin–paraffin deposits (ARPDs) was 81.7% and 95.4% for the Bulla-Deniz oil sample and 86.1% and 93.6% for the Muradkhanli oil sample, respectively. For surface tension reduction, the effectiveness was 63.3% and 77.6% for the first oil sample (Bulla-Deniz) and 84.3% and 73.6% for the second oil sample (Muradkhanli).
Experiments using the “cold finger” method were conducted over a three-hour period at the highly effective concentration of 600 g/t of the composition, across temperatures of 0 °C, 5 °C, 10 °C, 15 °C, 20 °C, 25 °C, and 30 °C. At each temperature, the amount of deposited oil sediments was measured using an analytical balance at intervals of 20, 40, 60, 80, 100, and 120 min (Table 12).
Table 12.
The amount of sediment deposited on the cold finger surface for Bulla-Deniz and Muradkhanli oils.
The inhibitory and bactericidal properties of the Marza-1 inhibitor and the ADM composition were investigated under laboratory conditions. The inhibitory properties were studied in aggressive corrosive environments containing hydrogen sulfide, carbon dioxide, and a combination of both gases. The laboratory tests were conducted at room temperature over a period of 6 h, and the results are presented in Table 13.
Table 13.
The protective effects of the Marza-1 inhibitor and the ADM composition in aggressive corrosive environments.
Based on the results of the laboratory studies, the protective effect of the Marza-1 inhibitor at concentrations of 3, 5, 7, and 10 mg/L in a H2S environment ranged from 90.3% to 98.1%, while the ADM composition at concentrations of 300, 400, 500, and 600 g/t exhibited a protective effect ranging from 94.6% to 99.9%, as shown in Table 7.
In a CO2 environment, these values were observed to be 80.1% to 96.1% for the inhibitor and 82.1% to 98.6% for the composition. Similarly, in a H2S + CO2 environment, the protective effect increased with the concentration, ranging from 87.6% to 94.2% for the inhibitor and 91.6% to 96.7% for the composition.
An analysis of the results indicates that the greatest protective effect was observed in the hydrogen sulfide environment. A comparative analysis of the results across all three aggressive environments confirmed that the ADM composition demonstrated a greater protective effect compared to the Marza-1 inhibitor. The best results were achieved at a concentration of 10 mg/L for the inhibitor and 600 g/t for the composition. Thus, the optimal concentration for the Marza-1 inhibitor is 10 mg/L, and, for the ADM composition, it is 600 g/t.
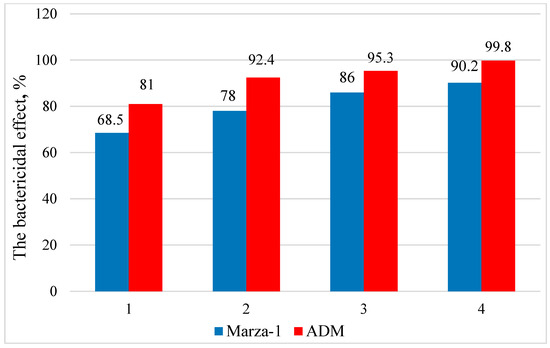
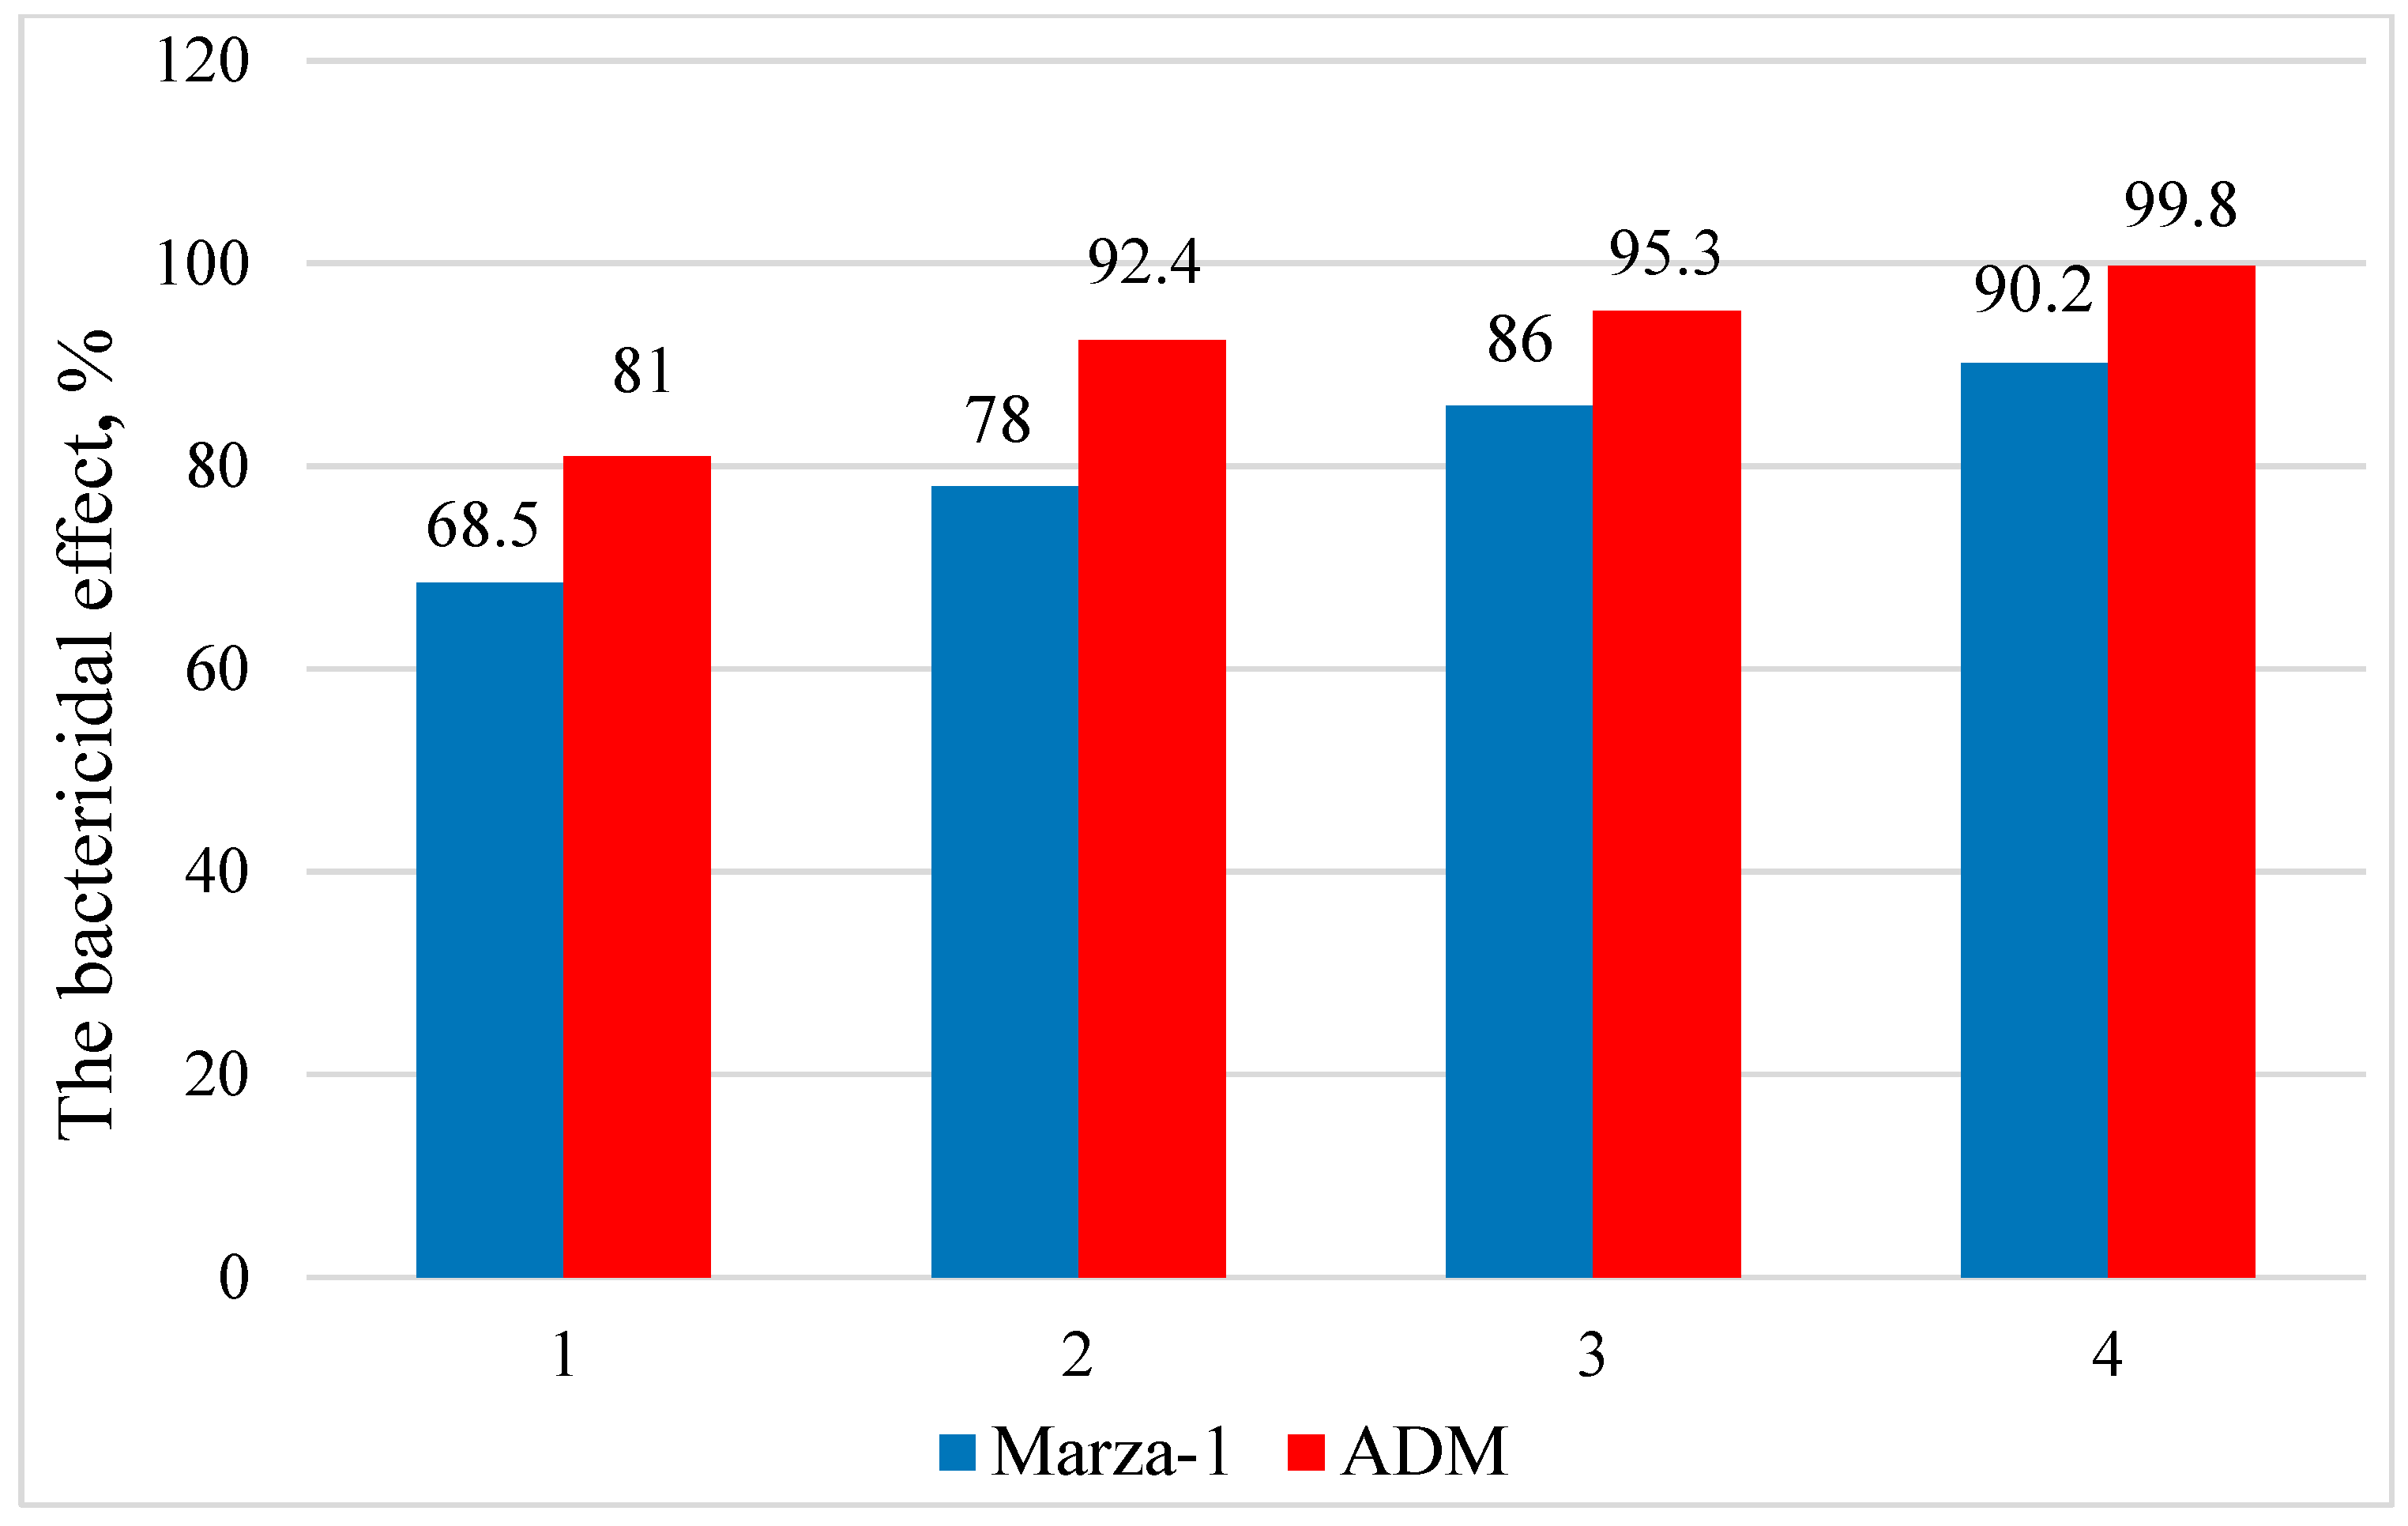
The bactericidal properties of the inhibitor and the composition were also determined through laboratory tests. Over a 15-day period in the Postgate-B nutrient medium, a significant reduction in the activity of two bacterial species, Desulfomicrobium and Desulfovibrio desulfuricans, was observed. The bactericidal effects of the Marza-1 inhibitor and the ADM composition were calculated based on changes in the hydrogen sulfide concentration (Figure 6).
Figure 6.
Bactericidal effect of the Marza-1 inhibitor (1–3; 2–5; 3–7; 4–10 mg/L) and the ADM reagent (1–300; 2–400; 3–500; 4–600 g/t) based on hydrogen sulfide content.
The bactericidal effect of the Marza-1 inhibitor at concentrations of 3, 5, 7, and 10 mg/L ranged from 68.5% to 90.2%, while the bactericidal effect of the ADM composition at concentrations of 300, 400, 500, and 600 g/t ranged from 81% to 99.8%, as shown in Figure 6. The strongest bactericidal effect was observed at the optimal concentration of 10 mg/L for the Marza-1 inhibitor and 600 g/t for the ADM composition. For 10 mg/L of the Marza-1 inhibitor, the bactericidal effect was 90.2%, while, for 600 g/t of the ADM composition, it reached 99.8%.
Thus, although both the inhibitor and the composition significantly reduced the amount of biogenic hydrogen sulfide in the Postgate B nutrient medium with sulfate-reducing bacteria, they did not completely halt the sulfate reduction process. However, by the seventh day of the experiments, the inhibitor had eliminated 90.2% and the composition had eliminated 99.8% of the sulfate-reducing bacteria, effectively halting their activity.
The optimal performance observed at a concentration of 600 g/t corresponds to the surface saturation of active components on water droplets, paraffin crystals, and metal surfaces. Below this concentration, incomplete surface coverage limits efficiency, while higher dosages do not provide proportional benefits due to adsorption equilibrium, making 600 g/t the optimal technical and economic dosage.
4. Discussion
4.1. Mechanistic Interpretation of the Synergistic Effect of the ADM Composition
The superior multifunctional performance of the ADM composition can be explained by the synergistic interaction of its individual components, Alkan-318, Difron-4201, and Marza-1, each of which targets a distinct physicochemical mechanism in oil production and transportation systems.
Alkan-318 primarily acts at the oil–water interface by reducing the interfacial tension and destabilizing the rigid interfacial films surrounding dispersed water droplets. This promotes droplet coalescence and accelerates phase separation, resulting in enhanced demulsification efficiency. Difron-4201 functions as a depressant additive by adsorbing onto the surfaces of paraffin crystals, modifying their crystallization behavior, suppressing crystal growth, and preventing the formation of an interconnected wax network. This mechanism leads to a reduced pour point and lower paraffin deposition tendencies.
Marza-1 contributes corrosion inhibition and bactericidal properties through adsorption on metal surfaces, forming a protective film that limits electrochemical reactions and inhibits the metabolic activity of sulfate-reducing bacteria. When combined in the ADM composition, these mechanisms reinforce one another: improved water separation reduces the electrochemical corrosion risk, inhibited paraffin deposition enhances flow conditions, and surface adsorption stabilizes the system against both chemical and biological degradation.
Similar synergistic effects have been reported for multifunctional oilfield chemicals combining demulsifying, inhibiting, and depressant functionalities, where cooperative interfacial, crystallization, and surface adsorption phenomena result in performance exceeding that of individual components [31].
4.2. Comparison with Commercial Multifunctional Oilfield Chemicals
The performance of the ADM composition compares favorably with that of multifunctional demulsifier–inhibitor–depressor formulations reported in the literature. Abdel-Azim et al. [32] reported demulsification efficiencies of 85–95% and corrosion protection levels of 90–97% for commercial oilfield chemicals under laboratory conditions. In contrast, the ADM composition achieved residual water content as low as 0.1–0.8%, corrosion protection efficiencies up to 99.9%, and ARPD inhibition exceeding 95% at comparable dosage levels.
These results indicate that the ADM composition is competitive with—and, in several performance indicators, superior to—existing commercial formulations, particularly for crude oils characterized by high water cut and elevated paraffin content. This highlights the industrial relevance of the proposed composition beyond laboratory-scale evaluation.
4.3. Environmental Considerations
From an environmental perspective, the reagents forming the ADM composition are applied at relatively low concentrations typical for oilfield chemical treatments. According to available safety classifications, Alkan-318 and Marza-1 belong to moderate hazard classes, while Difron-4201 is used at concentrations that minimize environmental loading. The multifunctional nature of the ADM composition enables the replacement of multiple single-function chemicals with a single formulation, potentially reducing overall chemical consumption and the associated environmental impacts.
Although a detailed life-cycle assessment and biodegradability analysis were beyond the scope of this study, the demonstrated efficiency at reduced dosage levels aligns with current trends toward more sustainable oilfield chemical technologies. Future work should include ecotoxicity and biodegradability testing in accordance with international environmental regulations governing oilfield chemical applications.
4.4. Practical Considerations and Field Implementation Limitations
Despite the promising laboratory results, several factors may influence the performance of the ADM composition under field conditions. Variations in temperature and pressure, changes in crude oil composition during long-term production, and prolonged exposure under continuous injection regimes may affect its chemical stability and adsorption behavior. Additionally, interactions with formation water chemistry, scale-forming ions, and flow regime variations could influence the overall efficiency.
Therefore, pilot-scale and field-scale trials under representative operating conditions are recommended to validate the laboratory findings and optimize injection strategies. Previous field studies have demonstrated that laboratory-validated multifunctional formulations can be successfully implemented in oilfield operations when adapted to reservoir-specific conditions [33,34].
4.5. Comparison with Multifunctional Oilfield Chemical Systems Reported in the Literature
The results obtained in this study are consistent with recent research on multifunctional oilfield chemical formulations designed to simultaneously address dehydration, corrosion inhibition, and deposit control. Previous studies have reported that combined demulsifier–inhibitor–depressor systems exhibit enhanced performance due to cooperative physicochemical mechanisms, particularly in high-water-cut and paraffinic crude oils [35,36].
Compared with the formulations discussed in these studies, the ADM composition demonstrates comparable or superior efficiency in terms of residual water reduction, asphaltene–resin–paraffin deposit inhibition, corrosion protection, and bactericidal activity, while operating at similar or lower dosage levels. This comparison confirms the industrial relevance of the ADM composition and supports its potential application as an alternative to existing multifunctional oilfield chemicals.
5. Conclusions
- Under laboratory conditions, for the first time, the effects of the “Alkan-318” demulsifier and ADM composition (“Alkan-318” + Difron-4201 + Marza-1 = 1:1:1) on the water cut factors of “Bulla-Deniz” oil with 75% water cut and Muradkhanli field oil with 41% water cut were studied. It was found that, at the optimal consumption concentration of 600 g/t for both the demulsifier and the composition, the water cut factor decreased to 0.1% for the first oil sample and to 0.8% for the second oil sample.
- At the optimal consumption rates of 900 g/t for the “Difron-4201” additive and 600 g/t for the ADM composition, the effectiveness in pour point reduction was 169.2% and 176.9% for the Bulla-Deniz oil and 151.4% and 170.0% for the Muradkhanli oil, respectively. The protection effectiveness against asphaltene–tar–paraffin deposits was 81.7% and 95.4% for the Bulla-Deniz oil sample and 86.1% and 93.6% for the Muradkhanli oil, respectively. For surface tension, this indicator was 63.3% and 77.6% for the first oil sample and 84.3% and 73.6% for the second oil sample, respectively.
- The effects of the Marza-1 inhibitor and ADM composition on the corrosion rate in formation water environments containing hydrogen sulfide, carbon dioxide, and a mixture of both gases, as well as on the vital activity of sulfate-reducing bacteria in “Postgate-B” medium, were studied. It was determined that, at the optimal consumption rate, the corrosion protection effectiveness was 98.1% and 99.9% in a hydrogen sulfide environment, 96.1% and 98.6% in a carbon dioxide environment, and 94.2% and 96.7% in a hydrogen sulfide and carbon dioxide environment, respectively. The bactericidal effects of the Marza-1 inhibitor and ADM composition were 90.2% and 99.8%, respectively.
- The superior multifunctional performance of the ADM composition is attributed to the synergistic interaction between its components, combining interfacial tension reduction, paraffin crystallization modification, and adsorption-based corrosion and bactericidal protection. This cooperative mechanism enhances its overall efficiency beyond that of individual reagents, as supported by the comparative performance data and mechanistic analysis presented in Section 4.
Author Contributions
Project administration, outline, structure, guidance, X.W.; supervision, expertise, data curation, visualization, writing—original draft preparation, X.W., M.A., and E.A.; experiments, E.A. All authors have read and agreed to the published version of the manuscript.
Funding
This research received no external funding.
Data Availability Statement
The original contributions presented in the study are included in the article; further inquiries can be directed to the corresponding author.
Conflicts of Interest
The authors declare no conflicts of interest.
References
- Wang, X.; Gurbanov, H.; Adygezalova, M.; Alizade, E. Investigation of removing asphaltene–resin–paraffin deposits by chemical method for Azerbaijan high-paraffin oil production process. Energies 2024, 17, 3622. [Google Scholar] [CrossRef] [Scilit]
- Wang, X.; Ismayilov, G.; Iskandarov, E.; Alizade, E.; Ismayilova, F. Study of specific problems arising in the blending processes of crude oils (based on the examples of Azerbaijan oils). Processes 2025, 13, 1500. [Google Scholar] [CrossRef] [Scilit]
- Panahov, G.M.; Abbasov, E.M.; Ismayilov, S.Z.; Huseynov, V.G. Development of new methods for combating asphaltene–resin–paraffin deposits. Azerbaijan Oil Ind. 2019, 1, 65–70. [Google Scholar]
- Mammad-Zade, A.M.; Alizade, E.F. Investigation of fluid dynamics impact with magnetic field applications on enhanced oil recovery in porous media. SOCAR Proc. 2025, 2, 61–67. [Google Scholar] [CrossRef] [Scilit]
- Nebogina, N.A.; Yudina, N.V. The influence of phase transitions in highly paraffinic oil and emulsions on structural and rheological properties. Petrochemistry 2020, 60, 511–519. [Google Scholar]
- Simon, S.; Theiler, S.; Knudsen, A.; Oye, G.; Sjöblom, J. Rheological properties of particle-stabilized emulsions. J. Dispers. Sci. Technol. 2010, 31, 632–640. [Google Scholar] [CrossRef] [Scilit]
- Hadi, A.A.; Ali, A.A. A review of petroleum emulsification types, formation factors, and demulsification methods. Mater. Today Proc. 2022, 53, 273–279. [Google Scholar] [CrossRef] [Scilit]
- Wang, Q.; Liu, Y.; Zhou, L.; Yang, S.; Gu, J.; Mu, B. An improved method for measuring the distribution of water droplets in crude oil based on optical microscopy technique. Laboratories 2025, 2, 1. [Google Scholar] [CrossRef] [Scilit]
- Adygezalova, M.B.; Ismayilov, G.G.; Babirov, K.N. Influence of heat treatment on the pour point of oil mixtures with different water content. In Proceedings of the International Seminar Dedicated to Professor G.V. Rassokhin, Ukhta, Russia, 4–5 February 2016; Volume I, pp. 251–254. [Google Scholar]
- ASTM D95-13(2018); Standard Test Method for Water in Petroleum Products and Bituminous Materials by Distillation. ASTM International: West Conshohocken, PA, USA, 2018.
- Zolfaghari, R.; Fakhru’l-Razi, A.; Abdullah, L.C.; Elnashaie, S.S.; Pendashteh, A. Demulsification techniques of water-in-oil and oil-in-water emulsions in petroleum industry. Sep. Purif. Technol. 2016, 170, 377–407. [Google Scholar] [CrossRef] [Scilit]
- Adeyanju, O.A.; Oyekunle, L.O. Optimization of chemical demulsification of water in crude oil emulsions. Egypt. J. Pet. 2019, 28, 349–353. [Google Scholar] [CrossRef] [Scilit]
- Gurbanov, H.R.; Qasimzade, A.V. Enhancing demulsification efficiency and corrosion protection in oil industry: A study of novel compositions. Voprosy Khim. Khim. Tekhnol. 2024, 2, 18–25. [Google Scholar] [CrossRef] [Scilit]
- Adygezalova, M.B. Research of demulsification and corrosion protection properties of a new multifunctional composition. Nafta-Gaz 2025, 4, 245–252. [Google Scholar] [CrossRef] [Scilit]
- Ashrafizadeh, S.N.; Motaee, E.; Hoshyargar, V. Emulsification of heavy crude oil in water by natural surfactants. J. Pet. Sci. Eng. 2012, 86–87, 137–143. [Google Scholar] [CrossRef] [Scilit]
- Puzikova, D.; Khussurova, G.; Leontyeva, X.; Kholkin, O.; Kenzin, N.; Zhurinov, M.; Peshaya, S. Review of organic corrosion inhibitors: Application with respect to main functional groups. J. Saudi Chem. Soc. 2025, 29, 20. [Google Scholar] [CrossRef] [Scilit]
- Norbutaeva, P. Protection of steel with corrosion inhibitors in hydrogen sulfide environments. Eurasian J. Phys. Chem. Math. 2022, 12, 83–87. [Google Scholar]
- Vigdorovich, V.I.; Tsygankova, L.E. Inhibition of Hydrogen Sulfide and Carbon Dioxide Corrosion of Metals; KARTEK Publishing: Moscow, Russia, 2011. [Google Scholar]
- Menshikov, I.A.; Shein, A.B. Protection properties of SOLING inhibitors in acidic hydrogen sulfide media. Chem. Chem. Technol. 2018, 61, 91–98. [Google Scholar]
- Gurbanov, H.R.; Pashayeva, S.M. Inhibitory effect of selected reagents on carbon steel corrosion in formation water containing hydrogen sulfide. Nafta-Gaz 2024, 1, 55–56. [Google Scholar] [CrossRef] [Scilit]
- GOST 2477-65; Petroleum and Petroleum Products—Method for Determination of Water Content. USSR Standard: Moscow, Russia, 1965.
- GOST 3900-85; Petroleum and Petroleum Products—Method for Determination of Density. USSR Standard: Moscow, Russia, 1985.
- GOST 33-2000; Petroleum Products—Determination of Kinematic Viscosity and Calculation of Dynamic Viscosity. Russian Standard: Moscow, Russia, 2000.
- GOST 11851-85; Petroleum—Method for Determination of Paraffin Content. USSR Standard: Moscow, Russia, 1985.
- GOST 1437-75; Petroleum Products—Method for Determination of Sulfur Content. USSR Standard: Moscow, Russia, 1975.
- GOST 20287-91; Petroleum Products—Method for Determination of Pour Point. USSR Standard: Moscow, Russia, 1991.
- GOST 4245-72; Drinking Water—Method for Determination of Chloride Content. USSR Standard: Moscow, Russia, 1972.
- GOST 11858-83; Petroleum and Petroleum Products—Method for Determination of Asphalt-Resin Content. USSR Standard: Moscow, Russia, 1966.
- GOST 12.1.007-76; Noxious Substances—Classification and General Safety Requirements. USSR Standard: Moscow, Russia, 1976.
- Tian, Y.S.; Yang, Z.Q.; Thoroddsen, S.T.; Elsaadawy, E. Image-based microfluidic method to test demulsifier enhancement of droplet coalescence rate. J. Pet. Sci. Eng. 2022, 208, 109720. [Google Scholar] [CrossRef] [Scilit]
- Saad, M.A.; Kamil, M.; Abdurahman, N.H.; Yunus, R.M.; Awad, O.I. Advances in demulsification techniques of crude oil emulsions. Processes 2019, 7, 470. [Google Scholar] [CrossRef] [Scilit]
- Abdel-Azim, A.A.; Mohamed, N.H.; El-Maghraby, A.A. Performance assessment of demulsifiers and corrosion inhibitors. Energy Fuels 2019, 33, 10562–10574. [Google Scholar]
- Wang, D.; Yang, D.; Huang, C.; Huang, Y.; Yang, D.; Zhang, H.; Liu, Q.; Tang, T.; El-Din, M.G.; Kemppi, T.; et al. Stabilization mechanism and chemical demulsification of water-in-oil and oil-in-water emulsions in petroleum industry. J. Pet. Sci. Eng. 2018, 165, 673–690. [Google Scholar] [CrossRef] [Scilit]
- Askari, M.; Aliofkhazraei, M.; Jafari, R.; Hamghalam, P.; Hajizadeh, A. Downhole corrosion inhibitors for oil and gas production—Review. Appl. Surf. Sci. Adv. 2021, 6, 100128. [Google Scholar] [CrossRef] [Scilit]
- Zhao, X.; Liu, Y.; Wang, J. Synergistic effects of multifunctional oilfield chemicals. J. Pet. Sci. Eng. 2021, 198, 108174. [Google Scholar]
- Lakkimsetty, N.R.; Gaddala, B.R.; Doddamani, D.; Thandlam, A.K.; Karu, C.V.; Namdeti, R.; Al Habsi, S. Reducing base sediment and water in crude oil separation. Fuel 2025, 397, 135478. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.