


Abstract
Digitalization of assembly processes represents a key pillar of Industry 4.0 and human-centered manufacturing, particularly in environments characterized by manual operations and high variability. This study experimentally compares traditional paper-based work instructions with a digital workflow created using Vuforia Capture. The objective is to assess the impact of instruction format on assembly performance in terms of time efficiency, error rate, and the need for external assistance when assembling an unfamiliar mechanical mechanism. An experimental study was conducted with participants lacking prior experience with the given assembly task. Two conditions were evaluated: assembly guided by paper documentation and assembly supported by step-by-step digital instructions. The measured indicators included total assembly time, number and type of errors, and assistance interventions. The results indicate substantial improvements when using digital instructions. Average assembly time decreased from 1084.8 s to 599.4 s (−44.75%), the total number of errors was reduced from 56 to 9 (−83.93%), and the need for assistance decreased from 58% to 2% of assembly steps. These findings suggest that digital work instructions significantly enhance user guidance, reduce cognitive load, and improve process stability, particularly for inexperienced users. The results should be interpreted with caution due to the limited sample size and controlled experimental conditions. Nevertheless, the study provides practical implications for practitioners and managers in manufacturing, as well as insights for researchers investigating digital instruction systems and training support tools in industrial environments.
1. Introduction
In the mechanical engineering industry, assembly processes belong to activities whose final quality is significantly influenced by the accuracy of work instructions, experience of the worker, and the latter’s ability to correctly interpret technical documentation. This influence is of special significance in conditions of a single-piece, small serial, or variant production, where assembly tasks consist of a high degree of manual labor and variability of operations and where they place requirements for increased spatial imagination of the user.
Traditional assembly procedures in industrial practice are based, in particular, on technical drawings, bills of material, instructional texts, and verbal instruction. The advantages of paper documentation are its easy availability, low technical requirements, and longstanding use in industrial environment [1,2].
However, in the training of new workers or inexperienced users, its utilization might pose a problem, as it requires independent interpretation of 2D technical documentation, correct parts identification, and understanding of their spatial orientation. In the case of an unfamiliar mechanism, this manner of work may prolong assembly time and lead to the occurrence of errors and an increased need for assistance [3,4].
Another limitation of paper documentation is its static nature. The user is forced to repeatedly switch attention between a drawing, a written instruction, physical components, and the assembly itself, which may increase cognitive load. Increased cognitive load may manifest in slower or less fluent execution of the assembly procedure [5,6].
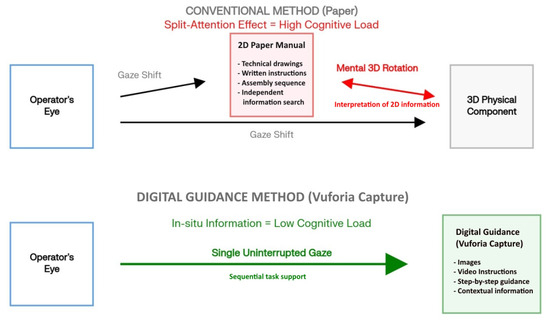
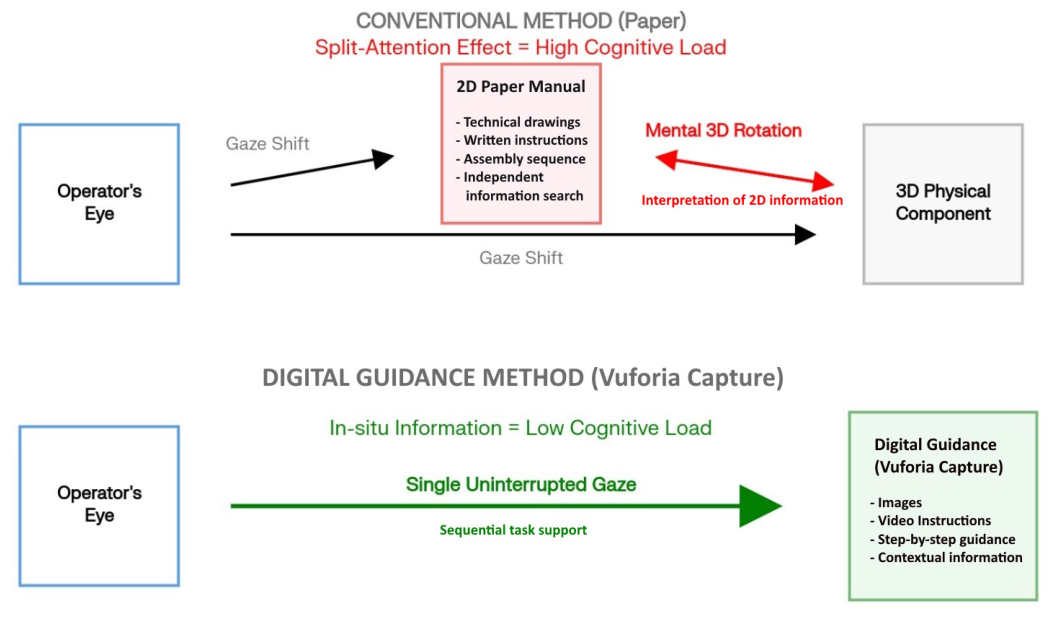
Figure 1 conceptually illustrates the difference in attention distribution between traditional paper-based instructions and mixed reality-supported assembly. In the case of paper documentation, the user’s attention is repeatedly shifted between multiple information sources, while mixed reality enables direct contextual visualization within the workspace, potentially reducing cognitive load.
Figure 1.
Conceptual comparison of attention distribution and information processing in conventional paper-based assembly guidance and tablet-based digital work instructions implemented using Vuforia Capture. The figure illustrates the split-attention effect and increased cognitive demands associated with paper documentation, compared with the contextual and sequential information support provided by digital guidance.
In the context of developing concepts of Industry 4.0, smart manufacturing and human-centered manufacturing, digital work instructions are the object of ever-increasing interest as a support tool of manual activities. Digital procedures make it possible to present work information in the form of a text, an image, a video, sound, or 3D models and provide the user with continuous guidance throughout the task execution [7,8]. Their benefit lies especially in their ability to guide the user on a step-by-step basis and to provide visual or checking support directly during assembly, which may contribute to the standardization of work procedures [9,10]. At the same time, digital instructions support more efficient knowledge transfer between experienced and less experienced workers [11].
Augmented and mixed reality technologies represent a significant approach to implementing digital work instructions directly in the environment of real assembly. Assembly information may be displayed in the context of a workstation, thus reducing the need for the interpretation of abstract technical documentation and, at the same time, improving the orientation of the user.
In industrial practice, these technologies are applied especially in assembly, maintenance, and servicing, as well as in the training of workers and in expert know-how transfer. Their utilization makes it possible to link digital content and the real work environment, thus creating a prerequisite for more effective execution of manual operations.
Research into digital, augmented, and mixed work instructions conducted so far has focused especially on their effect on the efficiency of manual assembly processes. Attention is focused especially on indicators such as assembly time, rate of error, cognitive load, the usability of technology, and the degree of user independence. Several studies point to the significance of supporting the user by guiding them through the work sequence and spatial orientation in the course of assembly [1,2]. Other works emphasize the benefit of digital and AR instructions in terms of error rate reduction and increased work efficiency [3,4], while other studies report similar findings in terms of error rate reduction [5,6]. At the same time, research results suggest that the efficacy of digital work instructions is significantly influenced by the manner of their implementation and the quality of the user interface.
A significant portion of research focuses on the use of digital and AR technologies in the area of workers training and practical skills transfer. These solutions enable a more effective conveyance of assembly and maintenance procedures while supporting adoption through visual and interactive user guidance. Studies point to the fact that AR training systems may improve the adoption of practical skills [7,8] and increase users’ independence in executing their work tasks [9,10]. At the same time, the importance of the user interface design and the manner of information presentation is emphasized, as they directly affect the adoption efficiency and quality of executed work [11].
An important area of research is the creation and management of digital and AR work instructions. Research focuses on how to effectively capture expert know-how and transform it into structured, user-friendly work procedures. Approaches based on “programming-by-demonstration” enable the creation of instructions directly from the execution of work tasks, thus reducing requirements for the manual creation of documentation [12,13]. At the same time, it appears that the efficiency of AR instructions depends on particular functions of the system, such as visual augmentation of steps, guidance of the user, or the checking of correct execution of operations [14,15,16]. A significant role is also played by visual element optimization and the amount of information presented, since too much information may increase cognitive load [17,18], especially when excessive information is presented [19].
Systematic and overview studies point to the fact that the efficiency of AR, VR, and MR work instructions depends on several factors, especially the nature of the task, the type of the imaging device, and the characteristics of the user group [20,21,22]. The results of those studies suggest that the benefit stemming from digital instructing systems cannot be deemed to be universal. Rather, it needs to be assessed in the context of a particular application. For this reason, experimental verification of individual solutions under real conditions is crucial for assessing their practical utilization.
Direct comparison of paper and digital or AR work instructions point to the fact that digital support may result in a reduced assembly time and error rate, especially when involving lesser-known, spatially demanding, or sequence-sensitive tasks. Several studies suggest that visual and interactive user guidance enables closer adherence to assembly sequence [23,24] and reduces the risk of incorrect interpretation of work steps [25]. This effect is especially pronounced in users lacking prior experience with the task at hand.
At the same time, experimental studies emphasize the significance of correct component identification, parts orientation, and adherence to assembly sequence, which have a crucial impact on the success of assembly operations. Digital and AR work instructions may provide effective support in this respect through visual guidance and contextual display of information, thus promoting error reduction [26,27] and improving workflow [28,29].
Other research covers digital work instruction assessment in various spheres of application, including time-critical assignments, training scenarios, and specific industrial conditions. The results of these studies highlight the importance of the context of use [30,31,32], and confirm that digital instructions may improve user orientation and reliability of executed operations [33,34,35].
It follows from available research that digital and AR work instructions have the potential to improve the efficiency of assembly processes, especially in terms of assembly time, error rate, and user support. However, this benefit cannot be deemed universal, as the end result depends on the context of a particular application and the nature of the assembly task.
That is why it is important to verify specific technological solutions experimentally in conditions corresponding to real deployment in the settings of mechanical engineering.
Despite the growing body of research addressing digital work instructions, evidence quantifying the practical effects of commercially available low-code industrial solutions such as Vuforia Capture in real mechanical engineering assembly contexts remains limited. This study addresses this gap by experimentally evaluating the magnitude of these effects under controlled conditions.
The contribution of this study does not lie in reconfirming the general benefits of digital work instructions, but rather in quantifying the magnitude of these effects for a specific implementation of Vuforia Capture and evaluating their practical significance within industrial practice. Accordingly, this study focuses on the use of Vuforia Capture, which enables the creation of digital work procedures directly from the real execution of assembly operations. The aim of the study is to experimentally compare traditional paper documentation with digital work procedures created using Vuforia Capture and to quantify their effects on selected assembly performance indicators.
Based on the aim above, the following research questions have been postulated:
- RQ1: Does the use of digital work instructions created in Vuforia Capture result in reduced assembly time compared to paper documentation?
- RQ2: Is there a smaller number of assembly errors using Vuforia Capture involving users lacking prior experience?
- RQ3: Does the digital work procedure reduce the need for additional assistance in the course of assembly?
- RQ4: Is the technology of Vuforia Capture a suitable training support tool in practical conditions of mechanical engineering?
2. Materials and Methods
Experimental verification focused on comparing two approaches to supporting the assembly process—the traditional paper documentation and the digital work procedure created in Vuforia Capture (version 3.25.0). The aim of the experiment was to analyze the influence of the form of the work instructions on the course of assembly, especially in terms of assembly time, error rate, and the need for additional assistance in executing assembly operations.
2.1. Experimental Workplace, Object of Assembly, and Technology Used
Experimental verification was conducted at the workplace set up for assembling a mechanical engineering subassembly of “Transmission board”, which constitutes a structurally significant mechanical unit of a servo drive. The choice of the subassembly was intentional, as it consists of several assembly steps necessitating correct part identification, adherence to assembly sequence, and precise component orientation.
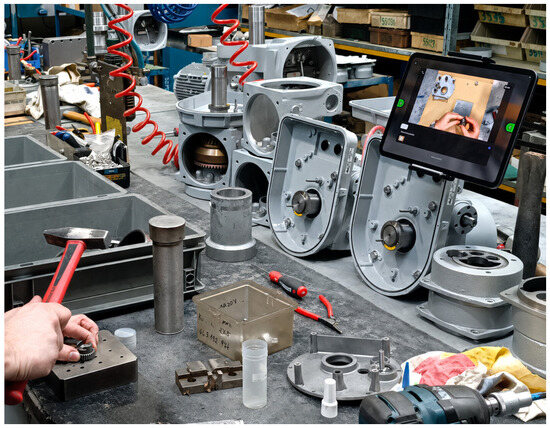
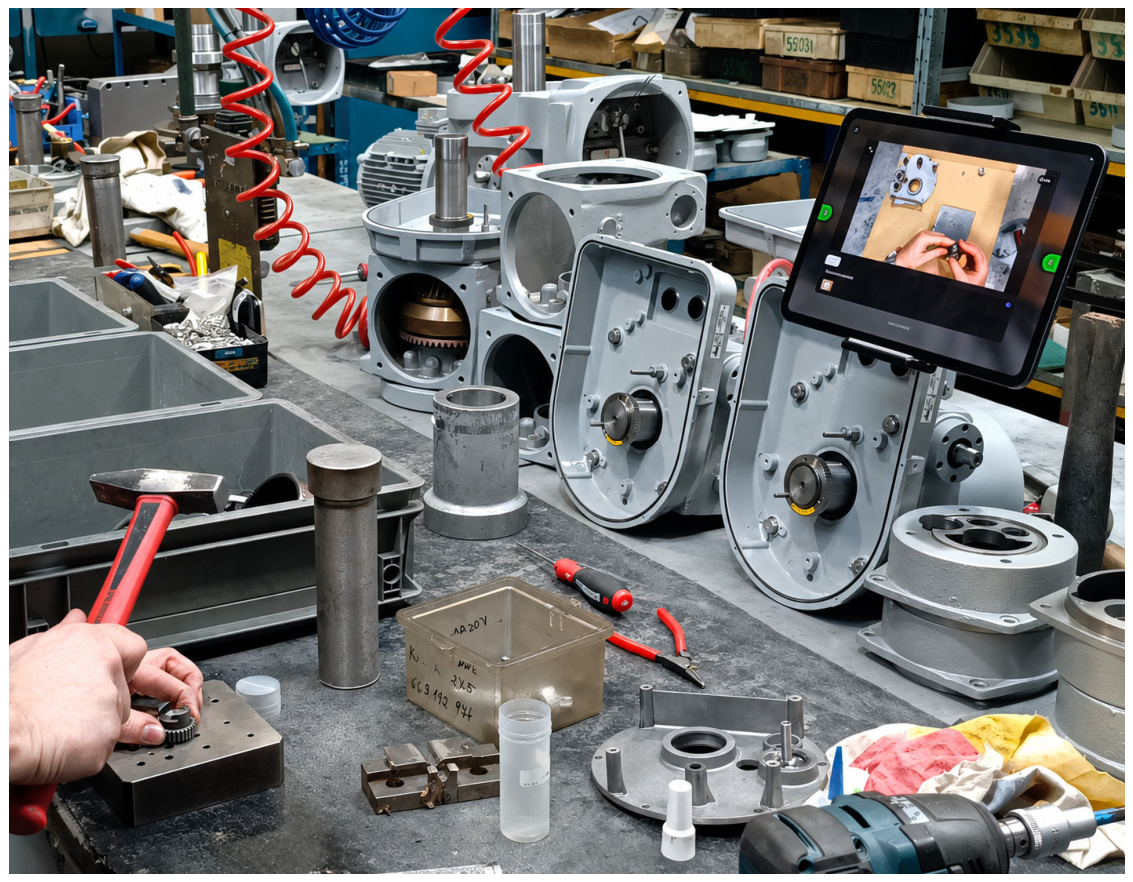
The workplace consisted of an assembly desk, a set of requisite components, tools, paper technical documentation, and a tablet with digital work procedure. An Apple iPad Pro tablet with a LiDAR sensor (Apple Inc., Cupertino, CA, USA) was used in the digital version of the experiment, displaying the sequential work procedure (Figure 2).
Figure 2.
Experimental assembly workplace used in the study. The figure illustrates the investigated transmission mechanism, the arrangement of the assembly components and tools, storage containers, and the integration of tablet-based digital work instructions within the assembly environment.
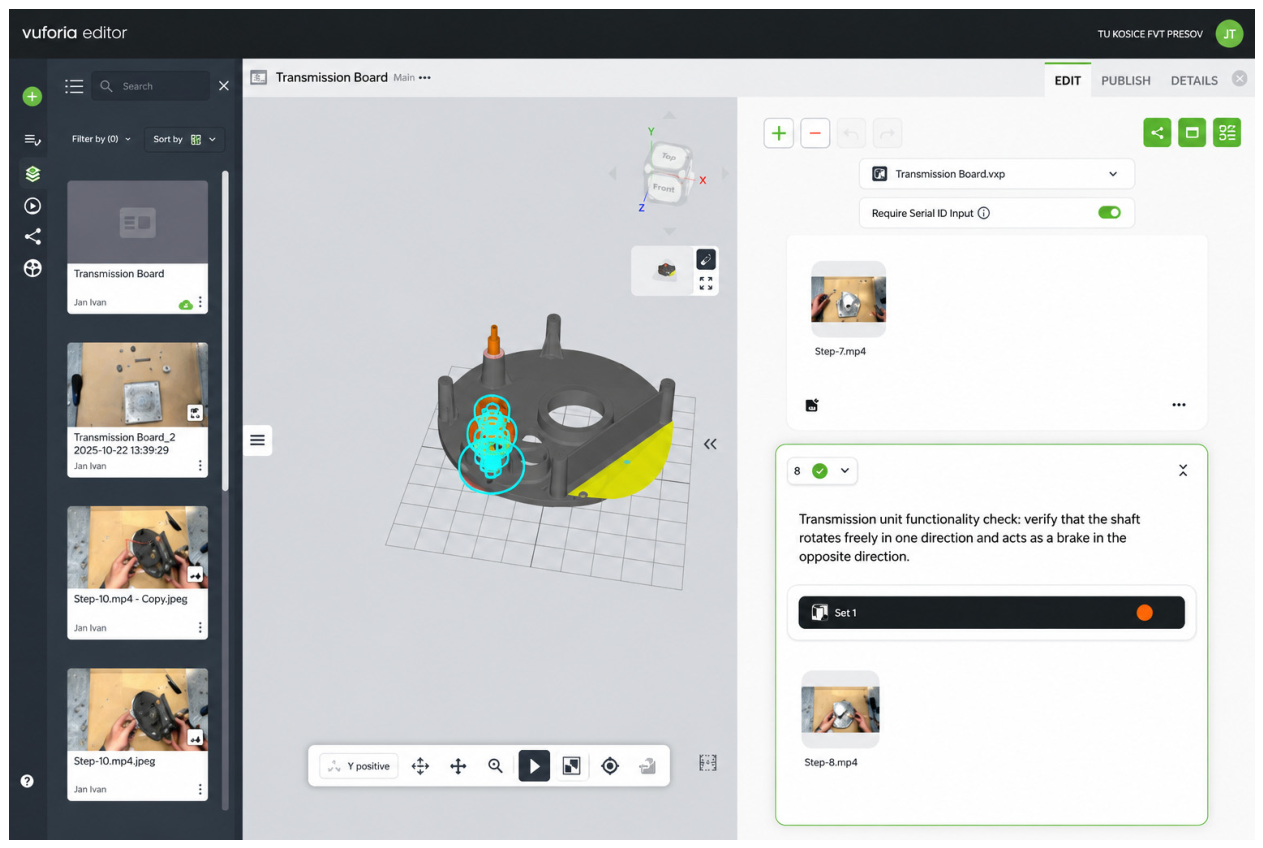
Vuforia Capture is a part of the Vuforia Expert Capture platform designated for recording, processing, and distributing work procedures. It makes it possible to capture the real work procedure, complement it with expert commentary, and transform it into sequential digital instructions. In the experiment, the assembly procedure was recorded with a tablet featuring a LiDAR sensor and then processed in Vuforia Editor (Figure 3). Individual steps were ordered into a logical sequence and completed with textual, image, and checking elements.
Figure 3.
Demonstration of a digital work procedure in Vuforia Editor. The colored overlays indicate highlighted assembly features and regions of interest used to guide the operator during task execution.
The digital work procedure contained text with instructions, reference images, video recordings, and graphic augmentation of critical spots, complete with checking steps to verify the correctness of individual component assembly. A procedure created in this way makes it possible to transform expert know-how into a repeatedly usable digital form, which may help to train users, support less experienced workers, and standardize assembly operations.
2.2. Research Sample and Experimental Versions
The research sample consisted of five employees from a mechanical engineering company who were involved in assembly-related activities. All participants possessed general technical knowledge and practical experience with routine assembly operations. However, none of them had previous practical experience with the specific transmission board assembly used in this study.
Detailed demographic characteristics were not recorded, as the primary objective of the participant selection was to ensure familiarity with routine assembly activities while excluding prior experience with the investigated assembly task and the evaluated digital work instruction system.
In addition, none of the participants had prior experience with Vuforia Capture or other digital work instruction systems. The selection of participants without familiarity with either the evaluated mechanism or the investigated digital solution was intentional, as the aim of the experiment was to assess the capability of different instruction formats to support users during their first encounter with an unfamiliar assembly procedure.
Experimental data were obtained from ten assembly cycles, where five cycles were executed using paper documentation and five cycles were supported with the digital work procedure in Vuforia Capture. Each cycle consisted of ten assembly steps, enabling the assessment of a total of 100 assembly operations. Due to the limited scope of the sample investigated, the results need to be interpreted as an indication of the potential benefit of technology and not as generally valid conclusions.
The assembly procedure consisted of ten sequential operations, including housing preparation, shaft insertion, bearing positioning, fastening operations, and functional verification. The sequence was selected to represent a realistic mechanical assembly requiring adherence to a prescribed order and correct component orientation.
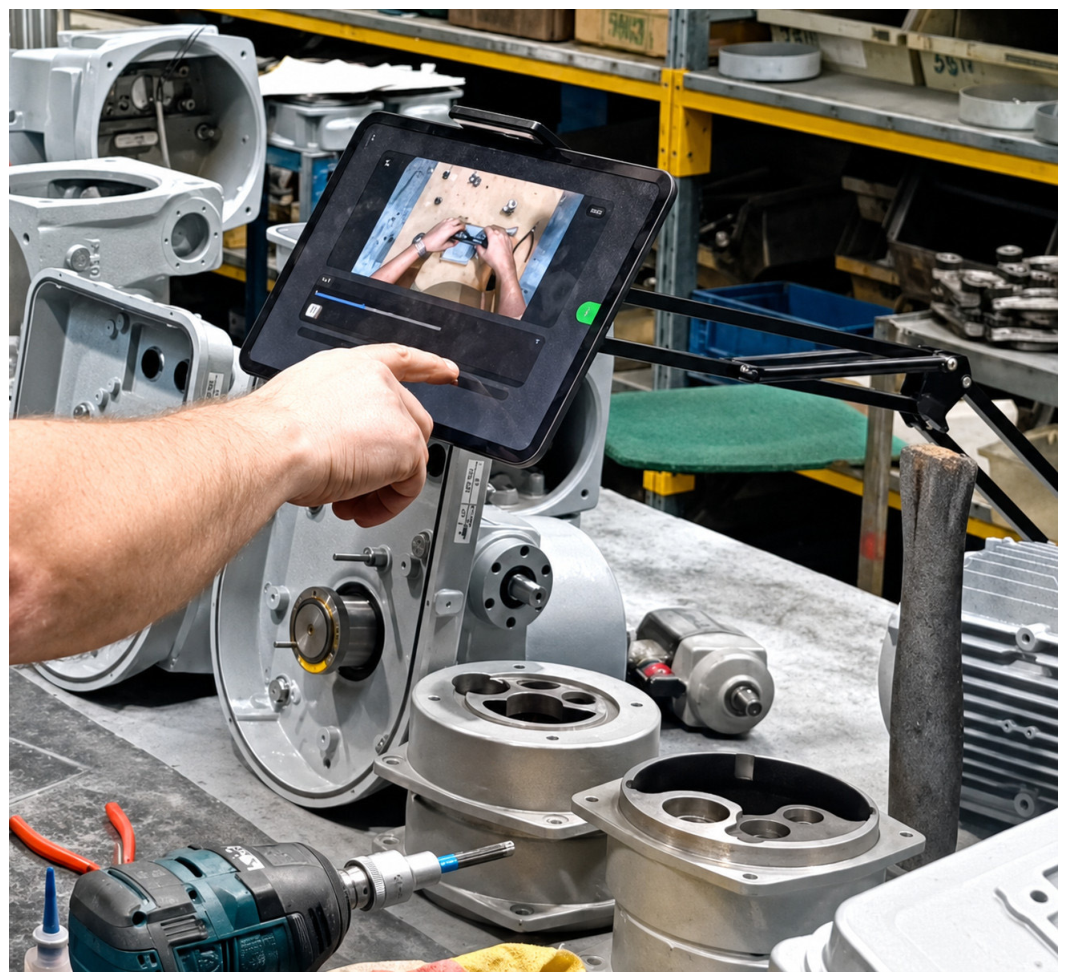
The experiment was designed as a comparison of two approaches to guiding assembly. The first version represented an assembly following paper documentation, where the participant had to interpret the technical drawing and identify individual steps on his own. The second version represented an assembly supported with a digital work procedure in Vuforia Capture, which provided sequential guidance step by step, with visual and checking support displayed on a tablet during the assembly process (Figure 4).
Figure 4.
Interaction with Vuforia Capture during the assembly process. The figure presents the use of tablet-based digital work instructions and illustrates how sequential visual guidance supported the operator throughout the investigated assembly task.
The experiment employed a repeated-measures design in which the same five participants completed the assembly task under both experimental conditions. To establish a baseline reflecting conventional industrial practice, all participants first performed the assembly using paper-based documentation. After completing this phase, the same participants carried out the assembly using the digital work instructions created in Vuforia Capture.
A potential limitation of the experimental design is that the fixed order of the experimental conditions may have introduced a learning effect, as participants became familiar with the assembly task during the first phase of the experiment. However, despite this possibility, the magnitude of the observed differences between the two conditions suggests that the improvements achieved with digital work instructions cannot be attributed solely to repeated task exposure. In particular, the assembly time decreased by 44.75%, the total number of recorded errors was reduced by 83.93%, and requests for external assistance decreased from 29 to 1 intervention.
Nevertheless, the absence of counterbalancing represents a methodological limitation of the study. Future research should employ randomized or counterbalanced experimental designs to isolate the effect of digital work instructions from potential practice-related improvements.
2.3. Investigated Indicators
Both quantitative and qualitative indicators were monitored during the experiment, focusing on assessing the course of assembly. The main parameters under assessment were the total assembly time, individual step time, number and type of errors, the need for additional assistance, and the clarity of the work procedure. An overview of the investigated indicators and the manner of their assessment is given in Table 1.
Table 1.
Investigated experiment indicators.
A standardized code list was used for consistent error typization, as listed in Table 2.
Table 2.
Assembly errors code list.
Assembly time was tracked from the first assembly step to completion of the last step. In addition to the total time, individual step times were also taken. The error count, error types, and the need for assistance were recorded through direct monitoring of the course of assembly. Error occurrence, error type, or eventual need for assistance by the monitoring personnel were recorded at each step.
In the digital version, the obtained data were completed with data from Vuforia Insights, which makes it possible to record the execution of the work procedure in its course, including the time data, and individual step completion.
Manually obtained data were used as a primary source of assessment, with data from Vuforia Insights serving to check the consistency of the measurements.
The combination of manual measuring and digital record increased the reliability of the experimental data. Manual monitoring made it possible to capture qualitative aspects of the course of assembly, while the digital record provided precise time data on the course of the work procedure.
In the case of paper documentation, data were obtained solely through direct measuring and monitoring, as no automated digital record was available.
2.4. Methods of Data Assessment
The obtained data were assessed with the use of descriptive statistics. Average values, minimums, maximums, and a standard deviation were established for the assembly time.
As for the error rate, the total error count, the average number of errors per participant, and the percentual reduction in error rate between the versions compared were assessed. The percentual reduction in assembly time was calculated from the equation below:
where represents the average assembly time with paper documentation and represents the average time using digital work procedure.
By analogy, the percentual reduction in error rate was calculated as follows:
where represents the total error count with paper documentation and represents the total error count following Vuforia.
Reduction in the need for assistance was expressed through a comparison of the number of assembly steps necessitating intervention by the monitoring personnel.
Due to the limited sample size of the experiment, the results are interpreted cautiously, and serve as an empirical indication of the potential contribution of the technology, not as generally valid conclusions. At the same time, in view of the nature of the experiment, no inferential statistical methods were applied, which represents a methodological limitation of the study. The mentioned limitations, however, do not impair the ability of the experiment to identify elemental differences between the approaches compared.
3. Results
Experimental comparison enabled the identification of differences between assembly following paper documentation and assembly supported by the digital work procedure in Vuforia Capture. The assessment focused on indicators related to the efficiency and reliability of the assembly, in particular the assembly time, error rate, and need for additional assistance.
3.1. Assembly Time
The measurement results point to a significant difference between the two assembly versions. Using paper documentation, the average assembly time was 1084.8 s (≈18 min 5 s), whereas using the digital work procedure in Vuforia Capture, the average time was 599.4 s (≈9 min 59 s).
The inter-version difference equaled 485.4 s, which accounts for an assembly time reduction by 44.75% in favor of the digital procedure.
Measurement results point to a significant difference between the two assembly versions, as listed in Table 3.
Table 3.
Assembly time comparison by assembly version.
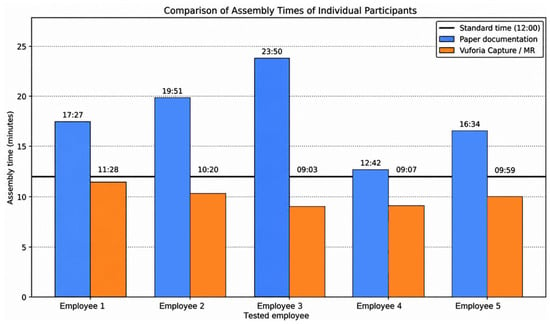
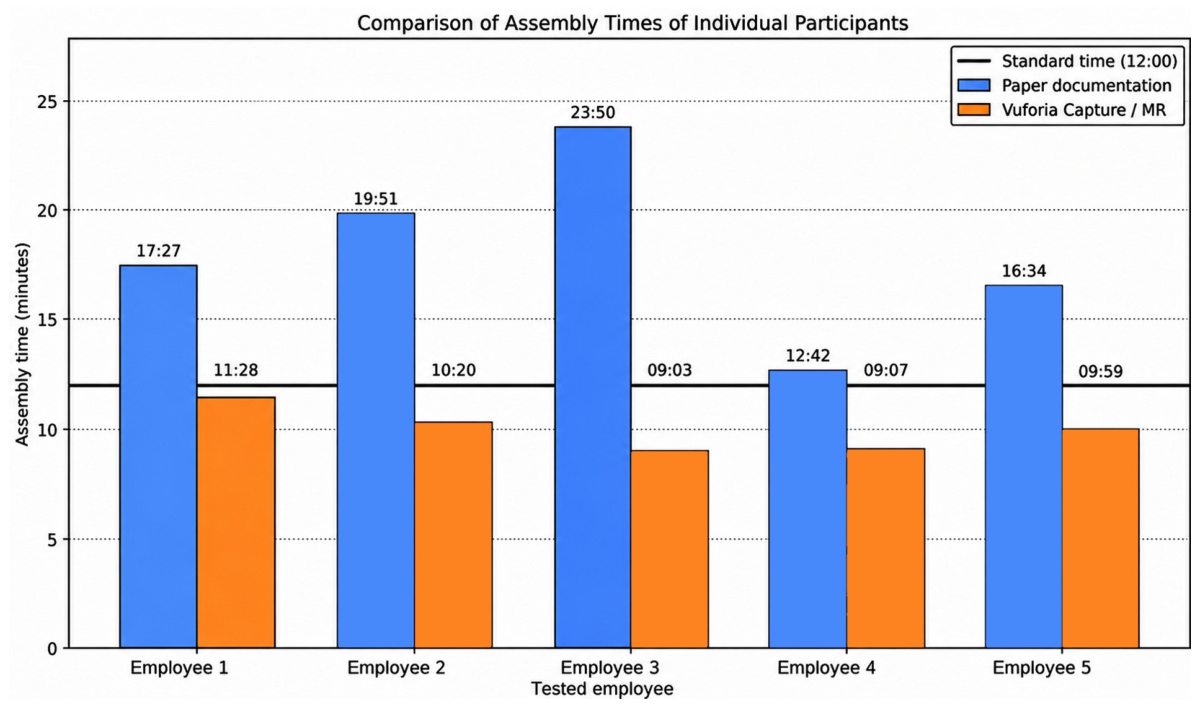
The use of paper documentation also correlated with greater assembly time variance (762–1430 s), whereas under digital procedure, the values were significantly more concentrated (543–688 s). This result hints at a more stable course of assembly when following digital instructions. Variance in assembly time of individual participants is shown in Figure 5.
Figure 5.
Comparison of assembly times of individual participants. Blue bars indicate assembly times using paper documentation, orange bars indicate assembly times using Vuforia Capture/MR, and the black horizontal line represents the standardized assembly time (12 min).
3.2. Comparison with Standardized Time
A standardized time of 12 min, which is 720 s, was set for the assembly task. In the case of paper documentation, all but one participant exceeded that time. In the case of Vuforia Capture/MR all participants completed assembly below the standardized time limit. Comparison of average and standardized time is shown in Table 4.
Table 4.
Comparison of average and standardized time.
It follows from the results that paper documentation failed to provide the majority of inexperienced participants with support that would be sufficient to complete the established standardized time limit. Conversely, proceeding digitally allowed assembly completion in a shorter time than the standard, which indicates its training support potential and acceleration of the assembly procedure.
3.3. Assembly Error Rate
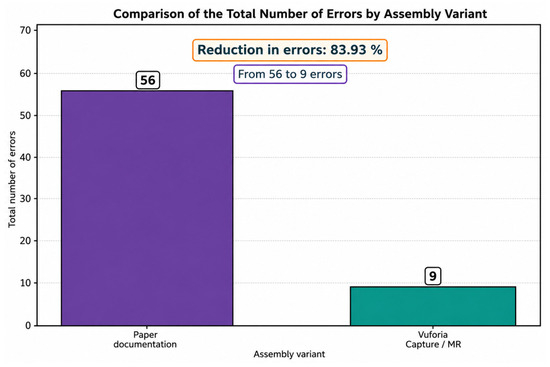
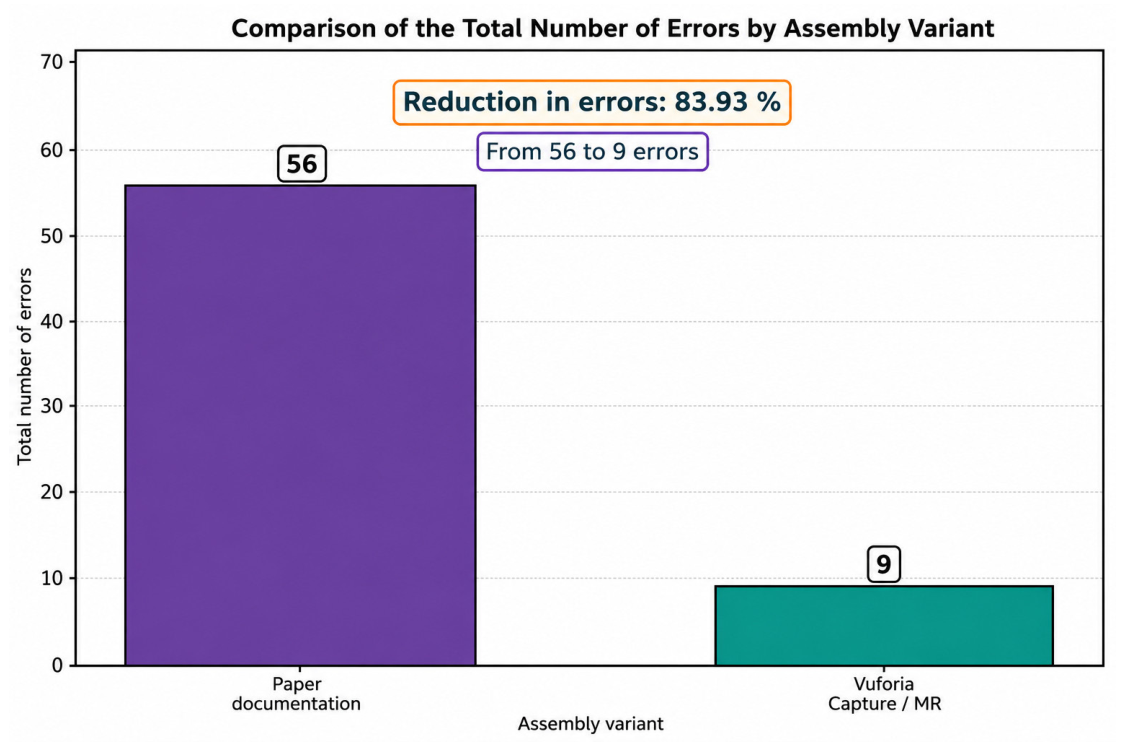
A total of 56 errors were recorded in the assembly following paper documentation, while only nine errors were recorded following the digital work procedure. Thus, the average number of errors per participant dropped from 11.2 to 1.8.
The percentual reduction in error rate was calculated as follows:
Thus, in the monitored sample, Vuforia Capture resulted in an overall error reduction of approximately 83.93%. The comparison of the experimental inter-version error rate is shown in Table 5.
Table 5.
Comparison of assembly error rate.
With paper documentation, the most frequently occurring errors related to incorrect mounting of parts, use of an incorrect component, and failure to follow the assembly sequence. With digital procedure, errors were less numerous and were mostly related to handling inaccuracy. This result suggests that visual guidance, image references, and checking mechanisms could help participants better understand the correct order and manner of execution of assembly steps. Figure 6 shows a comparison of the total error count plotted in graphs.
Figure 6.
Assembly inter-version error count compared.
3.4. Need for Additional Assistance
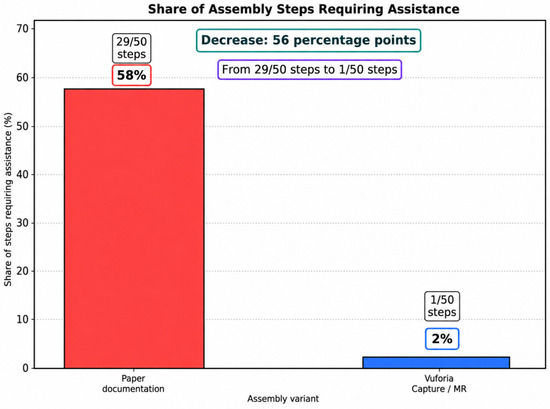
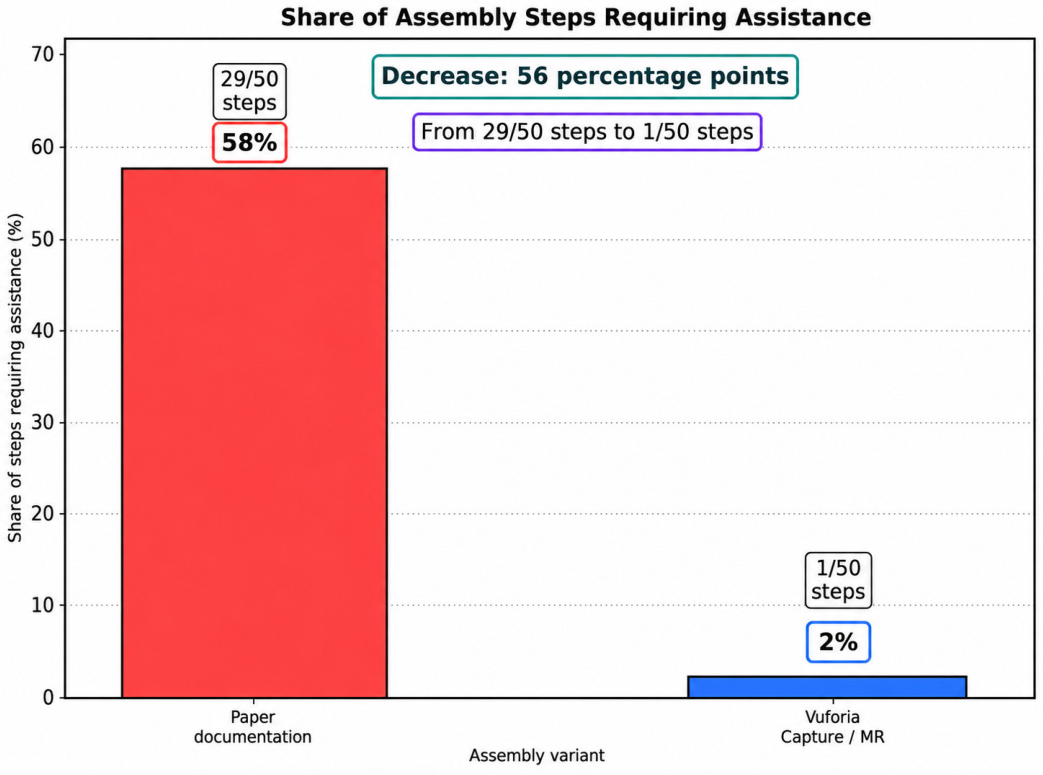
A significant difference was also found in assessing the need for external assistance. With paper documentation, assistance was needed in 29 out of 50 monitored assembly steps, which accounts for 58% of the steps. The digital work procedure significantly reduced the need for assistance (58% vs. 2%), as documented in Table 6.
Table 6.
Assembly version-dependent need for additional assistance.
This result points to a significantly higher degree of independence among participants when following a digital work procedure (Figure 7). While, with paper documentation, the participants often needed help with interpreting the procedure, identifying the parts, or deciding on the correct order of steps, following digital instructions, they were able to proceed mostly independently.
Figure 7.
Share of assembly steps requiring assistance.
3.5. Results Summary
A summary comparison of the experimental versions is shown in Table 7. The results consistently indicate a positive impact of the digital work procedure across all investigated indicators, with the most pronounced effects observed being in error reduction and reduced need for assistance.
Table 7.
Summary comparison of experimental versions.
4. Discussion
The experiment results point to a significant improvement in efficiency and reliability of the assembly when a digital work procedure created in Vuforia Capture is followed. The most pronounced effect was recorded in the area of error reduction and reduction in the need for additional assistance, which suggests that sequential digital guidance efficiently supports orientation of the user during the assembly of an unfamiliar mechanism.
The contribution of this study does not lie in demonstrating the existence of benefits associated with digital work instructions per se, but rather in quantifying these effects for a specific implementation of Vuforia Capture under experimentally controlled conditions relevant to mechanical engineering practice.
The reduction in assembly time (RQ1) may be explained, in particular, by the elimination of an independent search for and interpretation of information in technical documentation. This finding is consistent with previous studies reporting that digital and AR-supported work instructions facilitate faster task execution by reducing the need to interpret conventional documentation and search for task-relevant information [23,25]. The comparatively large reduction observed in this study may be related to participants’ unfamiliarity with the assembly task and the structured, step-by-step guidance provided by Vuforia Capture. The digital work procedure guides the user step by step, thus reducing the time needed for decision making and orientation in the assembly process. A significant finding is also lower inter-participant assembly time variance. This result suggests a higher degree of work procedure standardization and more stable work performance. In terms of industrial practice, this aspect is important, as performance repeatability and foreseeability are crucial for managing manufacturing processes.
In relation to the second research question, RQ2, a significant reduction in error occurrence has been confirmed. Digital work instructions ensure correct understanding of the assembly sequence and reduce the risk of incorrect part identification or order of operations. Similar observations have been reported in previous studies demonstrating that visual guidance and contextual information improve adherence to prescribed assembly sequences and reduce errors associated with incorrect part identification and orientation [26,27,29]. In line with these findings, the results from this study suggest that digital work instructions may be particularly valuable when users perform unfamiliar and sequence-dependent tasks.
The most pronounced difference was recorded in the need for additional assistance (RQ3). The digital work procedure resulted in a greater degree of user independence, which has significant practical implications, especially in the training of new workers. The reduced need for intervention by experienced personnel may contribute to a more effective use of human resources in industrial practice.
In relation to research question RQ4, it may be stated that Vuforia Capture technology is a suitable training support tool. Digital work procedures enable quicker adoption of assembly operations, reduce the cognitive load of the user, and support expert know-how transfer into digital form. This interpretation is supported by previous studies showing that AR-supported guidance can facilitate knowledge transfer and improve operator autonomy during skill acquisition [7,8,32]. From a human-centered manufacturing perspective, such systems may contribute to more efficient onboarding processes and enhanced workforce adaptability.
The established results correspond with published studies, which point to the positive impact of digital and AR work instructions on the efficiency of manual assembly tasks [23,24,25,26,27,28]. Although the sample size of this study was limited, the consistency of the observed trends with evidence synthesized in recent reviews and mapping studies increases confidence in the practical relevance of the findings [20,21,22]. Prior research identified a similar reduction of assembly time and error rate, especially with tasks requiring correct part orientation and adherence to assembly sequence. In this experiment, the difference was more pronounced, likely because the participants worked with an unfamiliar mechanism and had no prior practical experience with the task.
However, the obtained results cannot be interpreted as universally valid. Consequently, the findings from this study should primarily be interpreted as context-specific evidence derived from a particular assembly application rather than as universally transferable performance estimates. The efficiency of digital work instructions depends on the nature of the assembly task, the user group, and the manner of the system implementation, which has also been confirmed by several other studies [14,18,22]. Where simple or well-known operations are involved, the difference between paper and digital forms may be less pronounced, while with more complicated or lesser-known tasks, the benefit of digital support can be more significant.
The main limitations of the study include the small sample size and the involvement of participants who, despite possessing general assembly experience, were not directly evaluated under real production conditions. In addition, the experiment was conducted under controlled conditions using a single assembly task, which may limit the transferability of the findings to other industrial contexts. In real production environments, factors such as time pressure, workplace ergonomics, component availability, and organizational constraints may further influence the effectiveness of digital work instructions.
Another limitation relates to the repeated-measures design employed in this study. Since all participants first completed the assembly using paper-based documentation and subsequently performed the same task using digital work instructions, a learning effect cannot be entirely excluded. Although the substantial improvements observed across all investigated indicators suggest that the benefits of Vuforia Capture extend beyond simple task familiarization, future studies should adopt randomized or counterbalanced experimental designs to better isolate the effects of digital guidance.
Despite these limitations, the results suggest that Vuforia Capture technology may represent an effective tool supporting assembly processes, especially in the area of workers training, procedure standardization, and error rate reduction.
Future research should focus on verification of the results on a larger participant sample, in real industrial operation conditions, and on different types of assembly tasks. In addition, it would be appropriate to complete the assessment with inferential statistical methods, cognitive load analysis, and user experience evaluation.
5. Economic Analysis of Vuforia Capture Implementation
Economic evaluation was conducted as a preliminary and exploratory assessment of the potential costs and benefits associated with the implementation of digital work instructions in assembly processes. The objective was not to provide a comprehensive business case or a precise investment appraisal, but rather to illustrate the possible economic implications of the experimentally observed improvements under a set of simplified assumptions and model scenarios.
5.1. Starting Points of the Economic Analysis
The economic analysis draws on the experimentally established reduction in assembly time, error rate, and the need for additional assistance. Time savings per assembly corresponded to 485.4 s (0.1348 h). In addition, error count and assistance interventions dropped significantly, which may have an economic impact on production effectivity.
5.2. Investment and Operating Costs
Economic analysis included basic cost items necessary for the implementation of digital work instructions per assembly workstation. The main input costs include, in particular, the Vuforia Capture software license fee, the respective hardware, protective auxiliaries, and mounting of the imaging device.
Since the Vuforia Capture license fee is not publicly standardized, the economic model worked with an annual estimate of 2000 €/year. This value serves as a model input for framework economic analysis and may differ in practice depending on license conditions and the scope of deployment.
iPad Pro was used as the imaging device, proving itself suitable during the experiment in terms of stability of displaying and practical usability. The approximate purchase price of such a device ranges from 1100 to 1500 €.
The costs of mounting fixtures and auxiliaries depend on a particular solution and the level of mechanical resilience. A simple solution starts at about 50 €, while more robust industrial configurations may result in higher investment costs.
The main cost items considered in the economic model are summarized in Table 8. These values represent a ballpark model scenario and may differ depending on specific implementation conditions.
Table 8.
Cost items of technology implementation.
The basic scenario may start with the minimal configuration, consisting of the Vuforia Capture license, an iPad Pro tablet, a protective guard, and a holder. If deployed to meet the basic needs of a single workplace, the initial costs may be estimated to range between 3200 € and 3700 €. The model costs calculation is given in Table 9.
Table 9.
Model costs calculation.
The greatest share of the overall costs falls on the license fee. If a higher price-range tablet or a more mechanically resilient industrial holder were used, the initial investment could increase to 3600 € to 3900 €.
5.3. Economic Benefits of Implementation
Economic benefits were evaluated in terms of three main areas: assembly time reduction, error rate reduction, and reduction in the need for additional assistance.
Economic benefit from assembly time reduction may be calculated from the equation below:
where:
is annual benefit from time reduction,
is the number of assembly cycles per year,
is the time savings per assembly in hours,
is the worker’s hourly wage.
The experiment showed time savings of:
With a model hourly wage rate of a worker being 15 €/h, the savings per assembly are:
Financial savings depend on the worker’s hourly wage rate, as shown in Table 10.
Table 10.
Financial savings per assembly based on hourly labor cost.
The economic benefit from time reduction is relatively low compared to the savings resulting from error rate reduction. The reduction of assembly time itself may be economically significant, especially in a case involving a greater number of assembly cycles or a higher hourly wage rate for workers.
In addition to time savings, the economic benefit arising directly from an error rate reduction needs to be accounted for. Assembly errors may result in additional costs of repair, rework, quality control, extension of continuous production time or, in more serious cases, component damage.
In the experiment, the error count dropped from the average value of 11.2 errors per assembly with paper documentation to 1.8 error per assembly following a digital procedure. The average reduction amounted to 9.4 errors per assembly cycle.
The economic benefit of a reduced error rate may be expressed by the following equation:
where:
is annual benefit from error rate reduction;
is the number of assembly cycles per year;
is the average error count reduction per cycle;
is the average cost of a single error removal.
Since particular errors were not represented in financial terms in the experiment, it is appropriate to work with a calculation scenario.
The economic benefit from error rate reduction was analyzed using a scenario approach, as shown in Table 11.
Table 11.
Estimated financial savings based on reduction in assembly errors.
The results show that the economic benefit from an error rate reduction may significantly outweigh the savings resulting from a reduced assembly time. However, not every error recorded in the experiment would correspond to the same financial cost in real production. Some errors could have related to handling inaccuracy, repairable immediately, while others could have resulted in real rework or inspection costs.
Another significant benefit of the digital work procedure is the reduced need for external assistance. With paper documentation, assistance was needed in 29 out of 50 monitored steps, while, following a digital procedure, it was needed in only 1 of 50 steps. The average reduction corresponds to 5.6 assistance interventions per assembly cycle.
If one assistance intervention is assumed to last 1 min on average and is performed by a qualified worker whose hourly rate is 20 €/h, the savings per assembly are:
The economic benefit from a reduced need for assistance was analyzed based on different intervention length scenarios and hourly rates, as shown in Table 12.
Table 12.
Estimated financial savings from reduced need for assistance.
The benefit from reduced need for assistance is lower than that involving error rate, yet it has an important organizational impact. An experienced worker or a foreman does not need to be repeatedly disturbed while training less experienced workers, which may influence production flow and qualified personnel availability in a positive way.
5.4. Return of Investment Model
The overall economic benefit per assembly may be expressed as a sum of financial savings from a reduced assembly time, financial savings from a reduced error rate, and financial savings from a reduced need for assistance:
where:
is the overall benefit from one assembly;
is the benefit from reduced assembly time;
is the benefit from reduced error rate;
is the benefit from reduced need for assistance.
A conservative scenario may involve:
- worker’s hourly wage: 15 €/h;
- time savings per assembly: 2.02 €;
- cost per error: 1 €,
- reduced error rate savings: 9.40 €,
- savings on assistance: 1.40 €.
Total benefit per assembly:
With the costs of the first year standing at 3330 €, the ballpark payback point is:
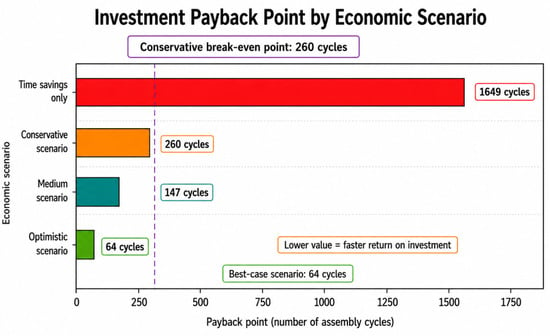
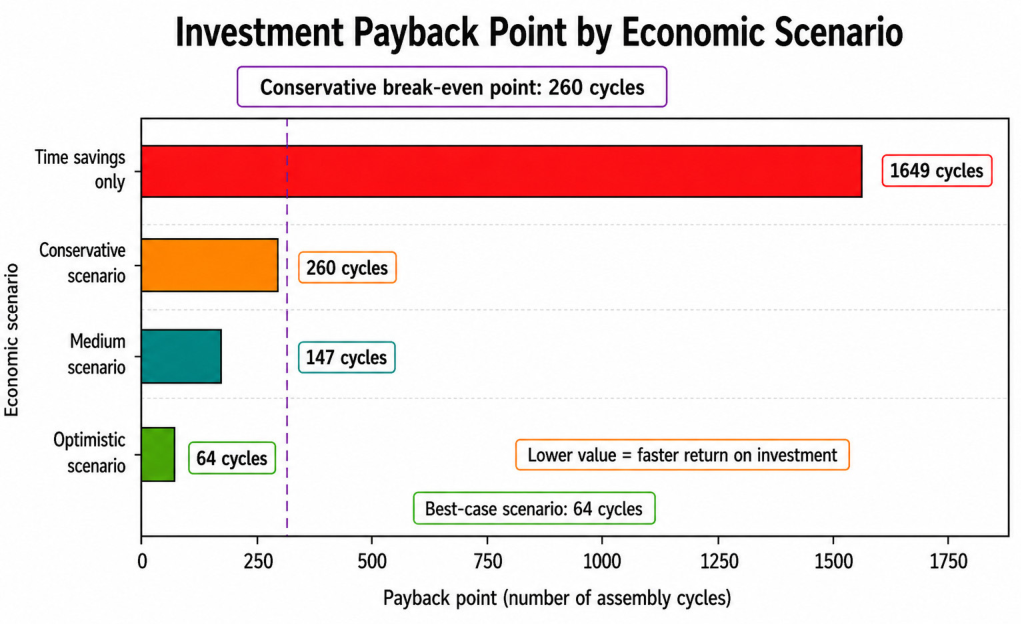
Under the conservative assumptions adopted in this exploratory analysis, the investment could potentially be recovered after approximately 260 assembly cycles. The return point model was analyzed through a scenario approach, as shown in Table 13, while the corresponding investment payback points for the individual scenarios are illustrated in Figure 8.
Table 13.
Return on investment (ROI) scenarios based on different levels of economic impact.
Figure 8.
Payback point of investment per economic scenario.
The results point to a significant impact of the error rate on economic return, where the return happens significantly faster when error costs are higher. The scenario evaluation shows that the return of investment strongly depends on the economic value of the errors removed and that of reduced need for assistance. If only time savings were evaluated, the return would be rather long. However, when the evaluation also accounts for errors and assistance, the return radically shortens.
5.5. Yearly Appreciation with Different Number of Assembly Cycles
For the sake of practical evaluation, a conservative scenario with savings of 12.82 € per assembly cycle was used. Yearly economic appreciation, depending on the number of assembly cycles, is shown in Table 14.
Table 14.
Yearly economic appreciation depending on the number of assembly cycles.
The scenario analysis suggests that economic return may be achievable at approximately 250 to 300 assembly cycles per year under the assumptions employed in this study. With a low number of cycles, the return is limited, while with greater utilization, the economic effect substantially grows.
It should be emphasized that the presented economic analysis is based on simplified assumptions regarding labor costs, error-related expenses, intervention duration, and implementation costs. These parameters may vary substantially across industrial sectors and individual enterprises. Consequently, the estimated savings and payback periods should be interpreted as illustrative scenarios rather than precise predictions of actual economic performance.
In subsequent years, where repeated hardware acquisition is not needed, the cost continues to be dominated by the license fee. At the cost of 2000 €/year, the payback point in the conservative scenario would correspond to:
This means that after the first year, the system could be economically beneficial at about 156 assembly cycles per year.
It follows from the results mentioned that the economic efficiency of implementation is significantly affected by the degree of utilization of the digital work procedure.
A more comprehensive economic evaluation would require long-term operational data obtained under real production conditions, including detailed records of quality costs, productivity indicators, maintenance requirements, and organizational factors influencing technology adoption.
5.6. Interpretation of Economic Appreciation
Economic appreciation points to the fact that implementation of Vuforia Capture is economically justifiable, especially in the case of assembly processes with a high frequency of repetition, higher costs of error removals, or demanding worker training.
If only time savings were assessed, the return of investment would be longer. However, in industrial practice, economic benefit results primarily from a reduced error rate and the need for assistance, which affect production quality, costs of repairs, and the effectiveness of training.
In assembling more difficult or costlier sets, even a relatively small reduction in error rates may have a significant economic impact. In such cases, the return of technology may be substantially faster than with simpler tasks, for which errors are low-cost.
It is also necessary to account for the costs of digital work procedure creation, which include the time of an expert, processing of the recording, and preparation of visual elements. However, with repeatable use, these costs are gradually split among a greater number of assembly cycles, thereby reducing unit costs. It follows from the mentioned results that the economic effectiveness of implementation is significantly subject to the degree of digital work procedure utilization.
Therefore, the economic findings should be regarded primarily as an indication of the potential economic attractiveness of digital work instructions rather than definitive evidence of their financial viability.
An expression of the estimated savings as a percentage of total product costs could provide additional practical insight into the economic significance of digital work instructions. However, detailed product-level costing data were not available within the scope of this study. Consequently, the economic assessment was intentionally limited to labor-related indicators and implementation costs derived from the experimentally observed improvements. Future studies should incorporate comprehensive product costing approaches to enable percentage-based evaluation of financial benefits.
6. Conclusions
The aim of the paper was to analyze Vuforia Capture technology as a tool supporting assembly procedures and to compare its efficiency with traditional paper documentation. Experimental verification was conducted on a group of users without prior experience with the mechanism to be assembled.
The results suggest that a digital work procedure created in Vuforia Capture may significantly contribute to increased effectiveness and reliability of the assembly process. Advantages included, primarily, the reduced assembly time, reduced error count, and a significant reduction in the need for additional assistance.
In practical terms, Vuforia Capture may be considered a prospective assembly supporting tool, especially in training less experienced workers, standardizing work procedures, and transferring expert know-how in the conditions of modern production.
Economic appreciation suggests that implementation of this technology is justified, especially in repeated assembly processes and tasks susceptible to a greater error rate. Significant portion of the economic benefit stems from reduced error count and need for assistance, rather than from the time reduction itself.
The results need to be interpreted in light of the limited sample size and experimental conditions investigated. At the same time, it is appropriate to complete the assessment with statistical methods and expand the analysis by the aspects of user experience and cognitive load.
Future research should aim to validate these findings by using larger and more diverse participant samples, including experienced operators and employees from different industrial sectors. Longitudinal studies examining the sustained effects of digital work instructions on learning retention, productivity, and error prevention would further enhance understanding of their long-term impact.
In addition, future investigations should evaluate the effectiveness of Vuforia Capture under different organizational and production contexts and compare its performance with alternative digital guidance solutions, including augmented reality and mixed reality systems employing different interaction paradigms. Finally, more comprehensive economic evaluations based on long-term operational data and detailed cost structures are needed to establish the financial implications of implementing digital work instructions in industrial practice.
Author Contributions
Conceptualization, J.I. and P.B.; methodology, J.I. and P.B.; software, J.M.; validation, J.M., J.I. and P.B.; formal analysis, J.I. and J.M.; investigation, J.I.; resources, J.I.; data curation, P.B. and J.M.; writing—original draft preparation, J.I. and P.B.; writing—review and editing, J.I. and P.B.; visualization, J.I.; supervision, J.M.; project administration, P.B.; funding acquisition, P.B. All authors have read and agreed to the published version of the manuscript.
Funding
The article was prepared thanks to the support of The Ministry of Education, Research, Development and Youth of the Slovak Republic through the grants KEGA number 009TUKE-4/2024. The article processing charge was funded by KEGA number 009TUKE-4/2024.
Institutional Review Board Statement
According to Slovak legislation (Act No. 576/2004 Coll. on healthcare and related services, as amended), ethical approval is not required for non-invasive research that does not involve medical procedures or the collection of personal or sensitive data. This study involved anonymous participants, no personal data collection, and posed no physical or psychological risk. Therefore, ethical approval was not required.
Informed Consent Statement
Informed consent was obtained from all subjects involved in the study.
Data Availability Statement
The data supporting the findings of this study are available from the corresponding authors upon reasonable request.
Conflicts of Interest
The authors declare no conflicts of interest.
References
- Wang, X.; Ong, S.K.; Nee, A.Y.C. A comprehensive survey of augmented reality assembly research. Adv. Manuf. 2016, 4, 1–22. [Google Scholar] [CrossRef] [Scilit]
- Wang, Z.B.; Ong, S.K.; Nee, A.Y.C. Augmented reality aided interactive manual assembly design. Int. J. Adv. Manuf. Technol. 2013, 69, 1311–1321. [Google Scholar] [CrossRef] [Scilit]
- Vanneste, P.; Huang, Y.; Park, J.Y.; Cornillie, F.; Decloedt, B.; Van den Noortgate, W. Cognitive support for assembly operations by means of augmented reality: An exploratory study. Int. J. Hum.-Comput. Stud. 2020, 143, 102480. [Google Scholar] [CrossRef] [Scilit]
- Rodriguez, F.S.; Saleem, K.; Spilski, J.; Lachmann, T. Performance differences between instructions on paper vs. digital glasses for a simple assembly task. Appl. Ergon. 2021, 94, 103423. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Drouot, M.; Le Bigot, N.; Bricard, E.; de Bougrenet, J.-L.; Nourrit, V. Augmented reality on industrial assembly line: Impact on effectiveness and mental workload. Appl. Ergon. 2022, 103, 103793. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Alessa, F.M.; Alhaag, M.H.; Al-Harkan, I.M.; Ramadan, M.Z.; Alqahtani, F.M. A neurophysiological evaluation of cognitive load during augmented reality interactions in various industrial maintenance and assembly tasks. Sensors 2023, 23, 7698. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Webel, S.; Bockholt, U.; Engelke, T.; Gavish, N.; Olbrich, M.; Preusche, C. An augmented reality training platform for assembly and maintenance skills. Robot. Auton. Syst. 2013, 61, 398–403. [Google Scholar] [CrossRef] [Scilit]
- Büttner, S.; Prilla, M.; Röcker, C. Augmented Reality Training for Industrial Assembly Work—Are Projection-Based AR Assistive Systems an Appropriate Tool for Assembly Training? In Proceedings of the CHI Conference on Human Factors in Computing Systems, Honolulu, HI, USA, 25–30 April 2020. [Google Scholar] [CrossRef] [Scilit]
- Gonzalez-Franco, M.; Pizarro, R.; Cermeron, J.; Li, K.; Thorn, J.; Hutabarat, W.; Tiwari, A.; Bermell-Garcia, P. Immersive mixed reality for manufacturing training. Front. Robot. AI 2017, 4, 3. [Google Scholar] [CrossRef] [Scilit]
- Qiu, C.; Zhou, S.; Liu, Z.; Gao, Q.; Tan, J. Digital assembly technology based on augmented reality and digital twins: A review. Virtual Real. Intell. Hardw. 2019, 1, 597–610. [Google Scholar] [CrossRef] [Scilit]
- Lai, Z.-H.; Tao, W.; Leu, M.C.; Yin, Z. Smart augmented reality instructional system for mechanical assembly towards worker-centered intelligent manufacturing. J. Manuf. Syst. 2020, 55, 69–81. [Google Scholar] [CrossRef] [Scilit]
- Kosch, T.; Knierim, P.; Kritzler, M.; Beicht, D.; Michahelles, F. Lenssembly: Authoring Assembly Instructions in Augmented Reality Using Programming-by-Demonstration. In Human-Technology Interaction; Springer: Cham, Switzerland, 2023; pp. 199–222. [Google Scholar] [CrossRef] [Scilit]
- Palmarini, R.; Fernández del Amo, I.; Ariansyah, D.; Khan, S.; Erkoyuncu, J.A.; Roy, R. Fast Augmented Reality Authoring: Fast Creation of AR Step-by-Step Procedures for Maintenance Operations. IEEE Access 2023, 11, 8407–8421. [Google Scholar] [CrossRef] [Scilit]
- Chu, C.-H.; Cheng, C.-Y.; Wu, C.-W. Comparing augmented reality-assisted assembly functions—A case study on Dougong structure. Appl. Sci. 2020, 10, 3383. [Google Scholar] [CrossRef] [Scilit]
- Dorloh, H.; Li, K.-W.; Chen, Y.-J.; Chen, C.-J.; Chen, S.-L. Presenting Job Instructions Using an Augmented Reality Device, a Printed Manual, and a Video Display for Assembly and Disassembly Tasks: What Are the Differences? Appl. Sci. 2023, 13, 2186. [Google Scholar] [CrossRef] [Scilit]
- Ojer, M.; Alvarez, H.; Serrano, I.; Saiz, F.A.; Barandiaran, I.; Aguinaga, D.; Querejeta, L.; Alejandro, D. Projection-based augmented reality assistance for manual electronic component assembly processes. Appl. Sci. 2020, 10, 796. [Google Scholar] [CrossRef] [Scilit]
- Neb, A.; Strieg, F. Generation of AR-enhanced assembly instructions based on assembly features. Procedia CIRP 2018, 72, 1118–1123. [Google Scholar] [CrossRef] [Scilit]
- Laviola, E.; Gattullo, M.; Manghisi, V.M.; Fiorentino, M.; Uva, A.E. Minimal AR: Visual asset optimization for the authoring of augmented reality work instructions in manufacturing. Int. J. Adv. Manuf. Technol. 2022, 119, 1769–1784. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Eswaran, M.; Varupala, P.S.S.V.; Hymavathi, M. Augmented reality guided autonomous assembly system: A novel framework for assembly sequence input validations and creation of virtual content for AR instructions development. J. Manuf. Syst. 2024, 72, 104–121. [Google Scholar] [CrossRef] [Scilit]
- Daling, L.M.; Schlittmeier, S.J. Effects of augmented reality-, virtual reality-, and mixed reality-based training on objective performance measures and subjective evaluations in manual assembly tasks: A scoping review. Hum. Factors 2024, 66, 589–626. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Peixe, L.C.; Agati, S.; Hounsell, M.S. Manual Assembly Augmented Reality Systems Implementation: A Systematic Literature Mapping. In Proceedings of the Symposium on Virtual and Augmented Reality, 2023; ACM: New York, NY, USA, 2024. [Google Scholar] [CrossRef] [Scilit]
- Wang, Z.; Bai, X.; Zhang, S.; Billinghurst, M.; He, W.; Wang, P.; Lan, W.; Min, H.; Chen, Y. A comprehensive review of augmented reality-based instruction in manual assembly, training and repair. Robot. Comput.-Integr. Manuf. 2022, 78, 102407. [Google Scholar] [CrossRef] [Scilit]
- Osman, S.; Eh Phon, D.N.; Omar, N.A.; Mohd Rameli, M.R.; Ahmad Alhassora, N.S.; Gusman, T. Using augmented reality application to reduce time completion and error rate in PC assembly. JOIV Int. J. Inform. Vis. 2020, 4, 166–171. [Google Scholar] [CrossRef] [Scilit]
- Kolla, S.S.V.K.; Sanchez, A.; Plapper, P. Comparing effectiveness of paper based and augmented reality instructions for manual assembly and training tasks. In Proceedings of the Conference on Learning Factories 2021, Online, 1–2 July 2021. [Google Scholar] [CrossRef] [Scilit]
- Eversberg, L.; Lambrecht, J. Evaluating digital work instructions with augmented reality versus paper-based documents for manual, object-specific repair tasks in a case study with experienced workers. Int. J. Adv. Manuf. Technol. 2023, 126, 1543–1559. [Google Scholar] [CrossRef] [Scilit]
- Uva, A.E.; Gattullo, M.; Manghisi, V.M.; Spagnulo, D.; Cascella, G.L.; Fiorentino, M. Evaluating the effectiveness of spatial augmented reality in smart manufacturing: A solution for manual working stations. Int. J. Adv. Manuf. Technol. 2018, 94, 509–521. [Google Scholar] [CrossRef] [Scilit]
- Tang, A.; Owen, C.; Biocca, F.; Mou, W. Comparative effectiveness of augmented reality in object assembly. In Proceedings of the CHI Conference on Human Factors in Computing Systems, Ft. Lauderdale, FL, USA, 5–10 April 2003; ACM: New York, NY, USA, 2003; pp. 73–80. [Google Scholar]
- Blattgerste, J.; Strenge, B.; Renner, P.; Pfeiffer, T.; Essig, K. Comparing conventional and augmented reality instructions for manual assembly tasks. In Proceedings of the PETRA Conference, Island of Rhodes, Greece, 21–23 June 2017; ACM: New York, NY, USA, 2017; pp. 75–82. [Google Scholar] [CrossRef] [Scilit]
- Hoover, M.; Miller, J.; Gilbert, S.; Winer, E. Measuring the performance impact of using the Microsoft HoloLens 1 to provide guided assembly work instructions. J. Comput. Inf. Sci. Eng. 2020, 20, 061001. [Google Scholar] [CrossRef] [Scilit]
- Illing, J.; Klinke, P.; Grünefeld, U.; Pfingsthorn, M.; Heuten, W. Time is money! Evaluating augmented reality instructions for time-critical assembly tasks. In Proceedings of the International Conference on Mobile and Ubiquitous Multimedia, Essen, Germany, 22–25 November 2020; ACM: New York, NY, USA, 2020; pp. 277–287. [Google Scholar] [CrossRef] [Scilit]
- Daling, L.M.; Tenbrock, M.; Isenhardt, I.; Schlittmeier, S.J. Assemble it like this!—Is AR- or VR-based training an effective alternative to video-based training in manual assembly? Appl. Ergon. 2023, 110, 104021. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Peltokorpi, J.; Hoedt, S.; Colman, T.; Rutten, K.; Aghezzaf, E.-H.; Cottyn, J. Manual assembly learning, disability, and instructions: An industrial experiment. Int. J. Prod. Res. 2023, 61, 7903–7921. [Google Scholar] [CrossRef] [Scilit]
- Chu, C.-H.; Ko, C.-H. An experimental study on augmented reality assisted manual assembly with occluded components. J. Manuf. Syst. 2021, 61, 685–695. [Google Scholar] [CrossRef] [Scilit]
- Platter, L.; Bernsteiner, R.; Kohlegger, M.; Ploder, C. Using augmented reality for work instructions: The impact on throughput time, error rate and cognitive load. In Proceedings of the KMO Conference, 2025; Springer: Cham, Switzerland, 2025; pp. 120–129. [Google Scholar] [CrossRef] [Scilit]
- Stanescu, A.; Mohr, P.; Thaler, F.; Kozinski, M.; Skreinig, L.R.; Schmalstieg, D.; Kalkofen, D. Error Management for Augmented Reality Assembly Instructions. In Proceedings of the 2024 IEEE International Symposium on Mixed and Augmented Reality, Seattle, WA, USA, 21 October 2024; IEEE: Piscataway, NJ, USA, 2024; pp. 690–699. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.