


Abstract
This study addresses the limited understanding of how build orientation and aggressive environments jointly affect the mechanical reliability of L-PBF 316L stainless steel. Specimens were fabricated in vertical, edge, and flat orientations and exposed for 360 h to 1 M H2SO4, 3.5 wt.% NaCl, and dry air oxidation at 800 °C. Tensile tests and microstructural analyses revealed strong anisotropy: edge and flat builds showed higher tensile and yield strength, while vertical builds exhibited greater ductility. Aqueous environments caused surface degradation and moderate strength loss, most severe in vertical samples. High-temperature oxidation induced σ-phase precipitation, increasing tensile strength (~20%) but reducing ductility and yield strength. These findings highlight the critical role of building orientation and service conditions in ensuring long-term performance of L-PBF 316L stainless steel.
1. Introduction
Additive manufacturing (AM) is a processing technology that combines computer-aided design with the layer-by-layer manufacturing strategy to produce near-net-shape components [1,2,3]. Particularly, laser powder bed fusion (L-PBF) is an AM technique that uses a high-power laser to melt metallic powders for a layer build-up technique [4]. This technology provides unique characteristics to the components that conventional manufacturing methods, such as casting or forging, cannot achieve. These characteristics involved design flexibility, manufacturing custom pieces with highly complex geometries, or high precision in forming. This processing technology also attracted significant attention due to its capacity to provide high-level densification [5], and high-performance metal parts without the necessity of post-processing treatments [6].
Among L-PBF processed materials, austenitic stainless steels (ss) are widely employed due to their high compatibility with the AM technology, high availability, excellent corrosion resistance and mechanical performance, and reasonable cost. Particularly, 316L ss is one of the most used due to its outstanding mechanical properties [7,8], high creep resistance [9], and excellent corrosion and oxidation resistance [10]. Because of these properties, 316L stainless steel is widely used in many industries, such as navigation, aerospace, chemical, pharmaceutical, petrochemical, and medical environments. In addition, its low carbon content (<0.03 wt.%) confers good weldability and makes the 316L ss an optimal grade for the L-PBF process [11].
The 316L ss parts manufactured by L-PBF typically reach high grain refinement and high dislocation density due to the high thermal gradient and cooling rate [12,13]. The high local energy and the fast scans are responsible for large thermal gradients and rapid solidification [14]. It produces higher tensile strength than conventionally manufactured pieces [15,16]. Suryawanshi et al. [17] found a significant enhancement in the yield strength of the L-PBF alloy compared with the conventional one due to the refinement in the microstructure, which results from the rapid solidification process. However, the mechanical behaviour of these parts is highly influenced by their anisotropic mechanical properties [18]. This anisotropy is attributed to many different factors related to the scan strategy, such as the direction of the grains, or the higher presence of inclusions, defects, or oxides in the interface between layers [19]. In this context, for an accurate investigation, it is necessary to analyse the mechanical behaviour of 316L ss parts based on the manufacturing orientation.
The corrosion behaviour of 316L ss manufactured by L-PBF has also been considered in the literature because the presence of segregations, thermal stresses inside the L-PBF parts, or irregular grains, can increase its tensile strength but negatively affect the corrosion performance [20,21,22]. In addition, defects, pores, and microstructural heterogeneities, intrinsic to the L-PBF process, can reduce corrosion and functional behaviour of L-PBF components [23]. In this context, pitting corrosion is one of the primary failure modes of these steels in chloride-rich environments [24,25]. Jingjing Nie et al. [26] compared the corrosion resistance of AM and wrought 316L ss in 3.5 wt.% NaCl solution and found that many sub-grain boundaries and high dislocation density in AM parts promoted the formation of a more compact and thicker passive film, but with a reduced self-repairing ability of the passive film. However, this 316L ss is not only limited to work in chloride-rich environments but also in acidic solutions [27,28,29] or high-temperature environments [30,31,32], among others. The 316L ss is recommended for high-temperature applications due to its excellent oxidation resistance, and, in this context, the parts manufactured by L-PBF increase their oxidation resistance compared with wrought samples [31,33]. However, again, the corrosion and oxidation resistance of L-PBF parts should be studied based on the manufacturing orientation due to their anisotropic behaviour [34,35,36].
Although previous studies have examined the mechanical properties or corrosion resistance of L-PBF 316L stainless steel individually, there is a lack of comprehensive research addressing how manufacturing orientation simultaneously influences both mechanical and corrosion behaviour under aggressive environments. This gap is critical because orientation-dependent anisotropy can significantly affect performance in real-life applications. The present work aims to fill this gap by systematically evaluating the combined effect of processing orientation and environmental exposure on the mechanical integrity of L-PBF 316L stainless steel. In this context, the relationship between the manufacturing orientation of L-PBF parts and their corrosion properties has been evaluated in three aggressive environments to analyse their influence on mechanical properties: (i) 1 M H2SO4 water solution, (ii) 3.5 wt.% NaCl water solution, and (iii) oxidation at high temperature in dry air at 800 °C. These different conditions allow a deep and complete study of the role that aggressive environments play on mechanical behaviour and how selecting the proper processing orientation could improve the mechanical performance of the L-PBF 316L ss exposed to real-life simulated conditions.
2. Materials and Methods
2.1. Base Materials
The 316L austenitic ss was manufactured by L-PBF and provided by Idonial Co. (Gijón, Spain). The L-PBF system was equipped with a fibre laser EOS M280 400W (Munich, Germany), and the main parameters used during the manufacturing process are shown in Table 1. The particle size of the initial 316L ss powders was 20 to 50 μm, and their composition was 17.0 Cr, 13.1 Ni, 2.7 Mo, 1.3 Mn, 1.2 Si, and Bal. Fe (in wt.%).
Table 1.
Main parameters used during the L-PBF process.
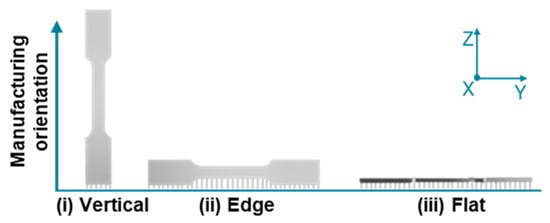
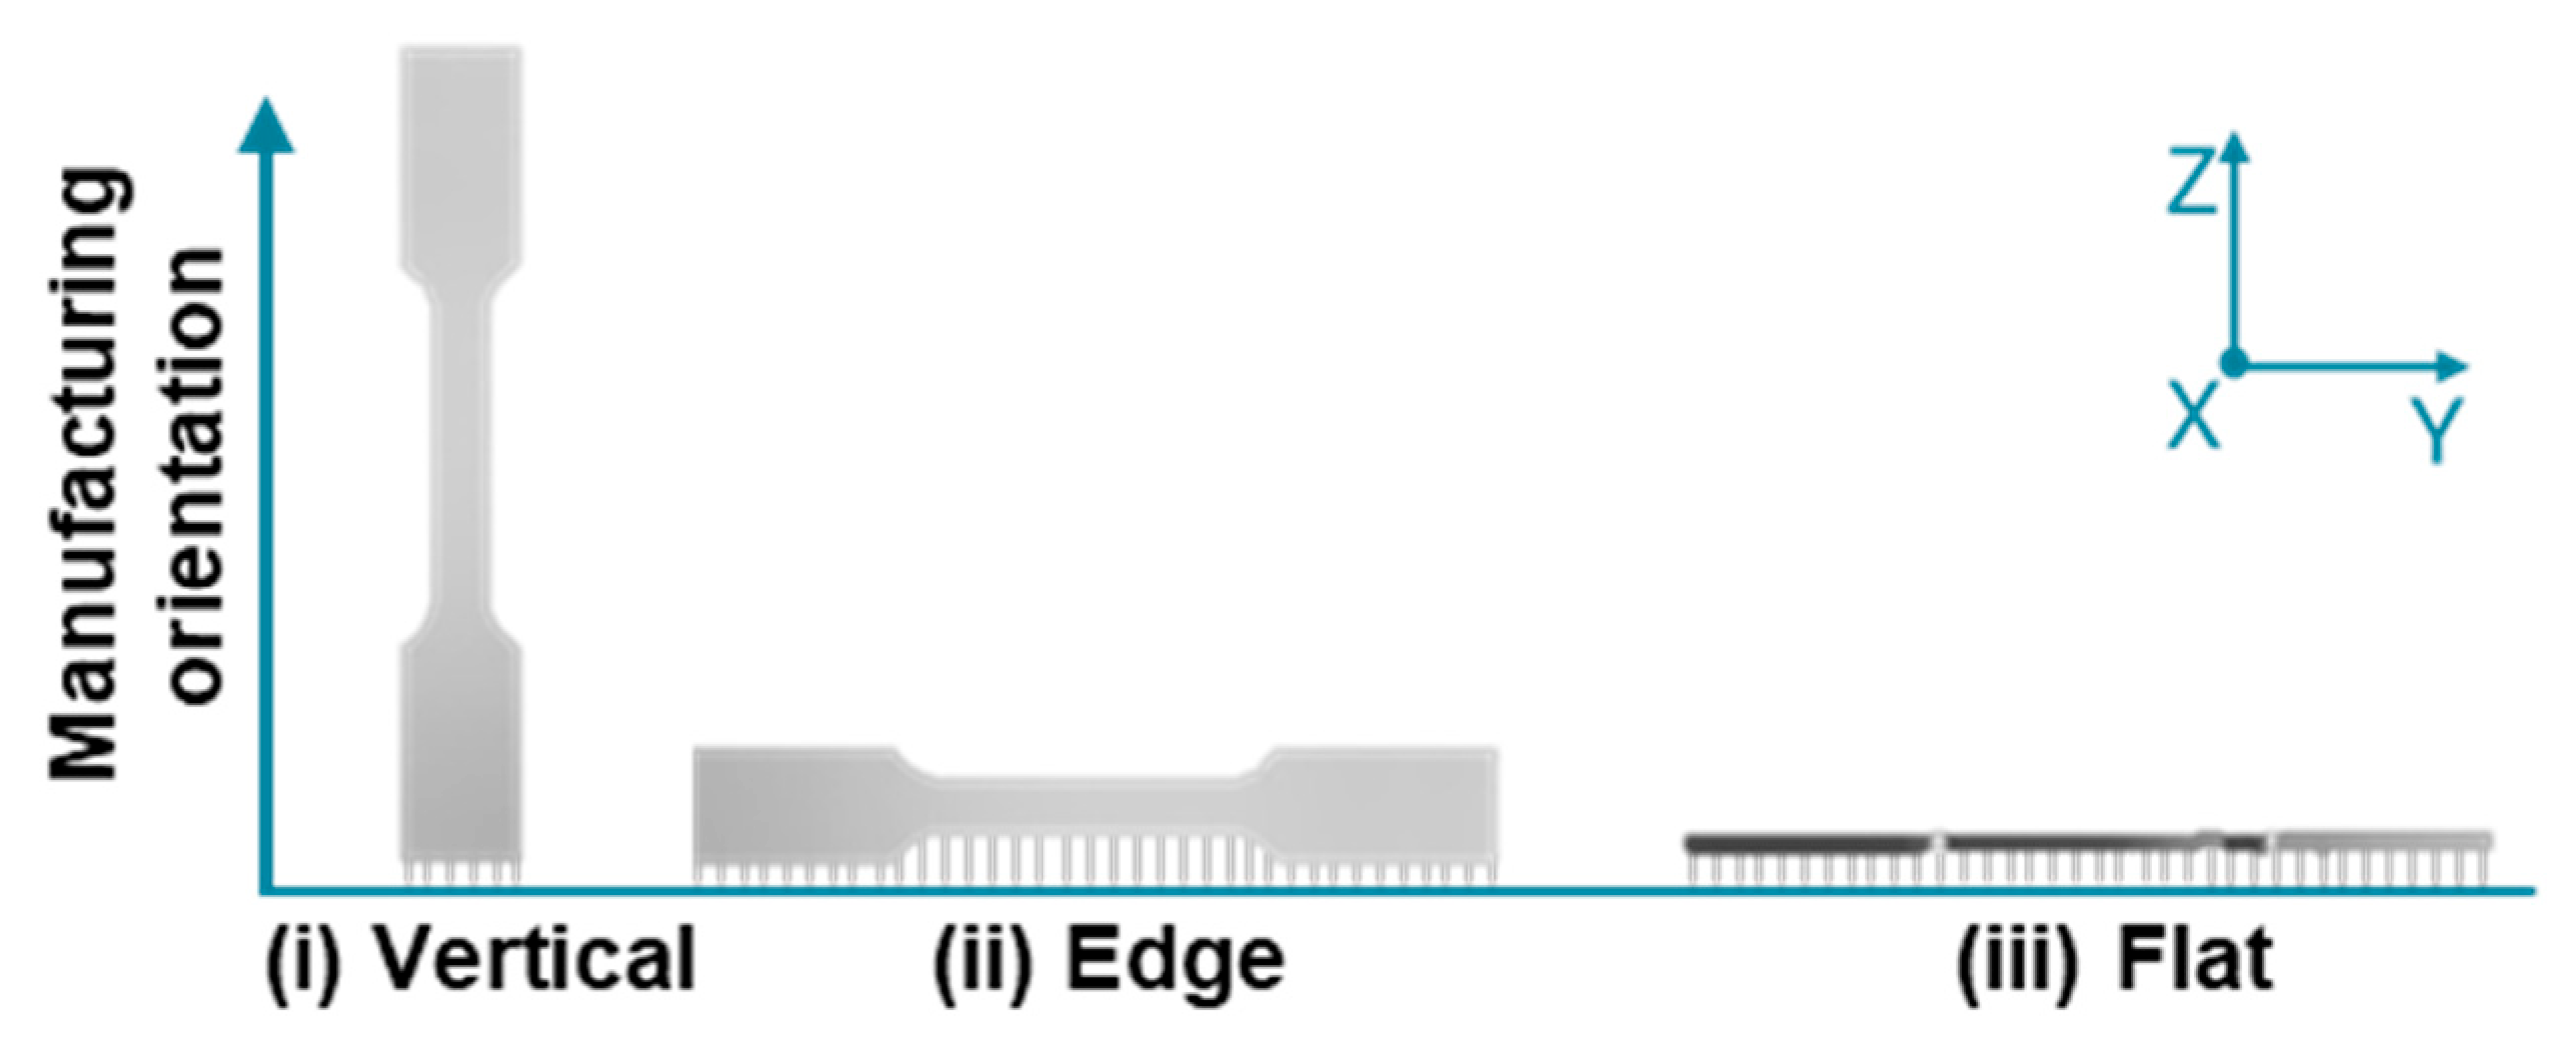
Normalised samples for tensile tests were manufactured by L-PBF with a 6 × 2 mm2 section and 82 mm length. Three different manufacturing orientations were employed to analyse their influence on the mechanical properties. Figure 1 shows a scheme of the employed orientations: (i) vertical (V), (ii) edge (E), and (iii) flat (F). The nomenclature used to refer to the as-built samples in function of their orientation was 316L-V, 316L-E, and 316L-F, respectively. This configuration was used to perform tensile strength tests considering build orientation-induced mechanical anisotropy in L-PBF pieces [37,38].
Figure 1.
Scheme of the employed L-PBF manufacturing orientations: (i) vertical, (ii) edge, and (iii) flat.
2.2. Corrosion Tests
The L-PBF 316L ss samples were exposed to different environments in the as-built condition without surface treatment. The aggressive environments used were: (i) immersion test in H2SO4 solution (1 M) at room temperature, which was prepared from analytical grade chemicals and distilled water, (ii) immersion test in NaCl solution (3.5 wt.%) at room temperature, and (iii) high-temperature oxidation test at 800 °C in a dry air atmosphere using a Nabertherm LT 5/12/P330 furnace (Lilienthal, Germany). These three different tests were performed for 360 h to analyse their influence on the mechanical behaviour of the 316L ss. The nomenclature used to refer to the samples exposed to these environments was 316L-H2SO4, 316L-NaCl, and 316L-O, respectively.
2.3. Mechanical Tests
Tensile tests were carried out at 2 mm/min speed in a ZWICK/ROEL type 8594.60 testing machine (Ulm, Germany) equipped with a MakroXtens II extensometer (Ulm, Germany) following ISO 6892-1 standard [39]. Tensile strength and elongation were measured for each specimen, and four samples were used for each experimental condition to guarantee the reproducibility of tensile strength results. The nomenclature used for each experimental condition is shown in Table 2, according to the processing orientation (vertical, edge, or flat) and the exposed aggressive environment (1 M H2SO4 solution (H2SO4), 3.5 wt.% NaCl solution (NaCl), or high-temperature oxidation (O)). A total of twelve conditions were analysed, including those used as reference.
Table 2.
Sample nomenclature according to manufacturing orientation (vertical, edge, or flat) and the exposed aggressive environment (1 M H2SO4 solution, 3.5 wt.% NaCl solution, or high-temperature oxidation).
Samples were tested in the as-built condition without any polishing or surface treatment to retain the characteristic roughness of L-PBF parts and assess their effect on mechanical degradation after environmental exposure.
2.4. Characterisation Methods
The as-built L-PBF 316L ss was microstructurally characterised using a Leica (Wetzlar, Germany) DMR optical microscope (OM) and a Hitachi (Tokyo. Japan) S3400N scanning electron microscope (SEM). The effect of the different aggressive environments on the exposed surface or sample microstructure was also analysed in cross-section using the same techniques. The samples were prepared by cutting metallographic pieces using a SiC disc cutter, mounting in resin, grinding with SiC emery paper up to 4000 grade, and polishing with diamond paste to 1 µm. Finally, the samples were etched with Vilella’s reagent to reveal their microstructure. The SEM analysis was also used to characterise the fractured surfaces after tensile strength tests, and semi-quantitative compositional analyses were carried out using energy dispersive X-ray spectroscopy (EDX) with a Bruker XFlash 5010 detector (Billerica, MA, USA).
3. Results
3.1. As-Built Materials Characterisation
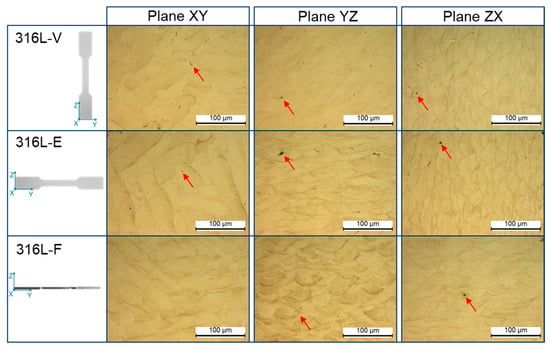
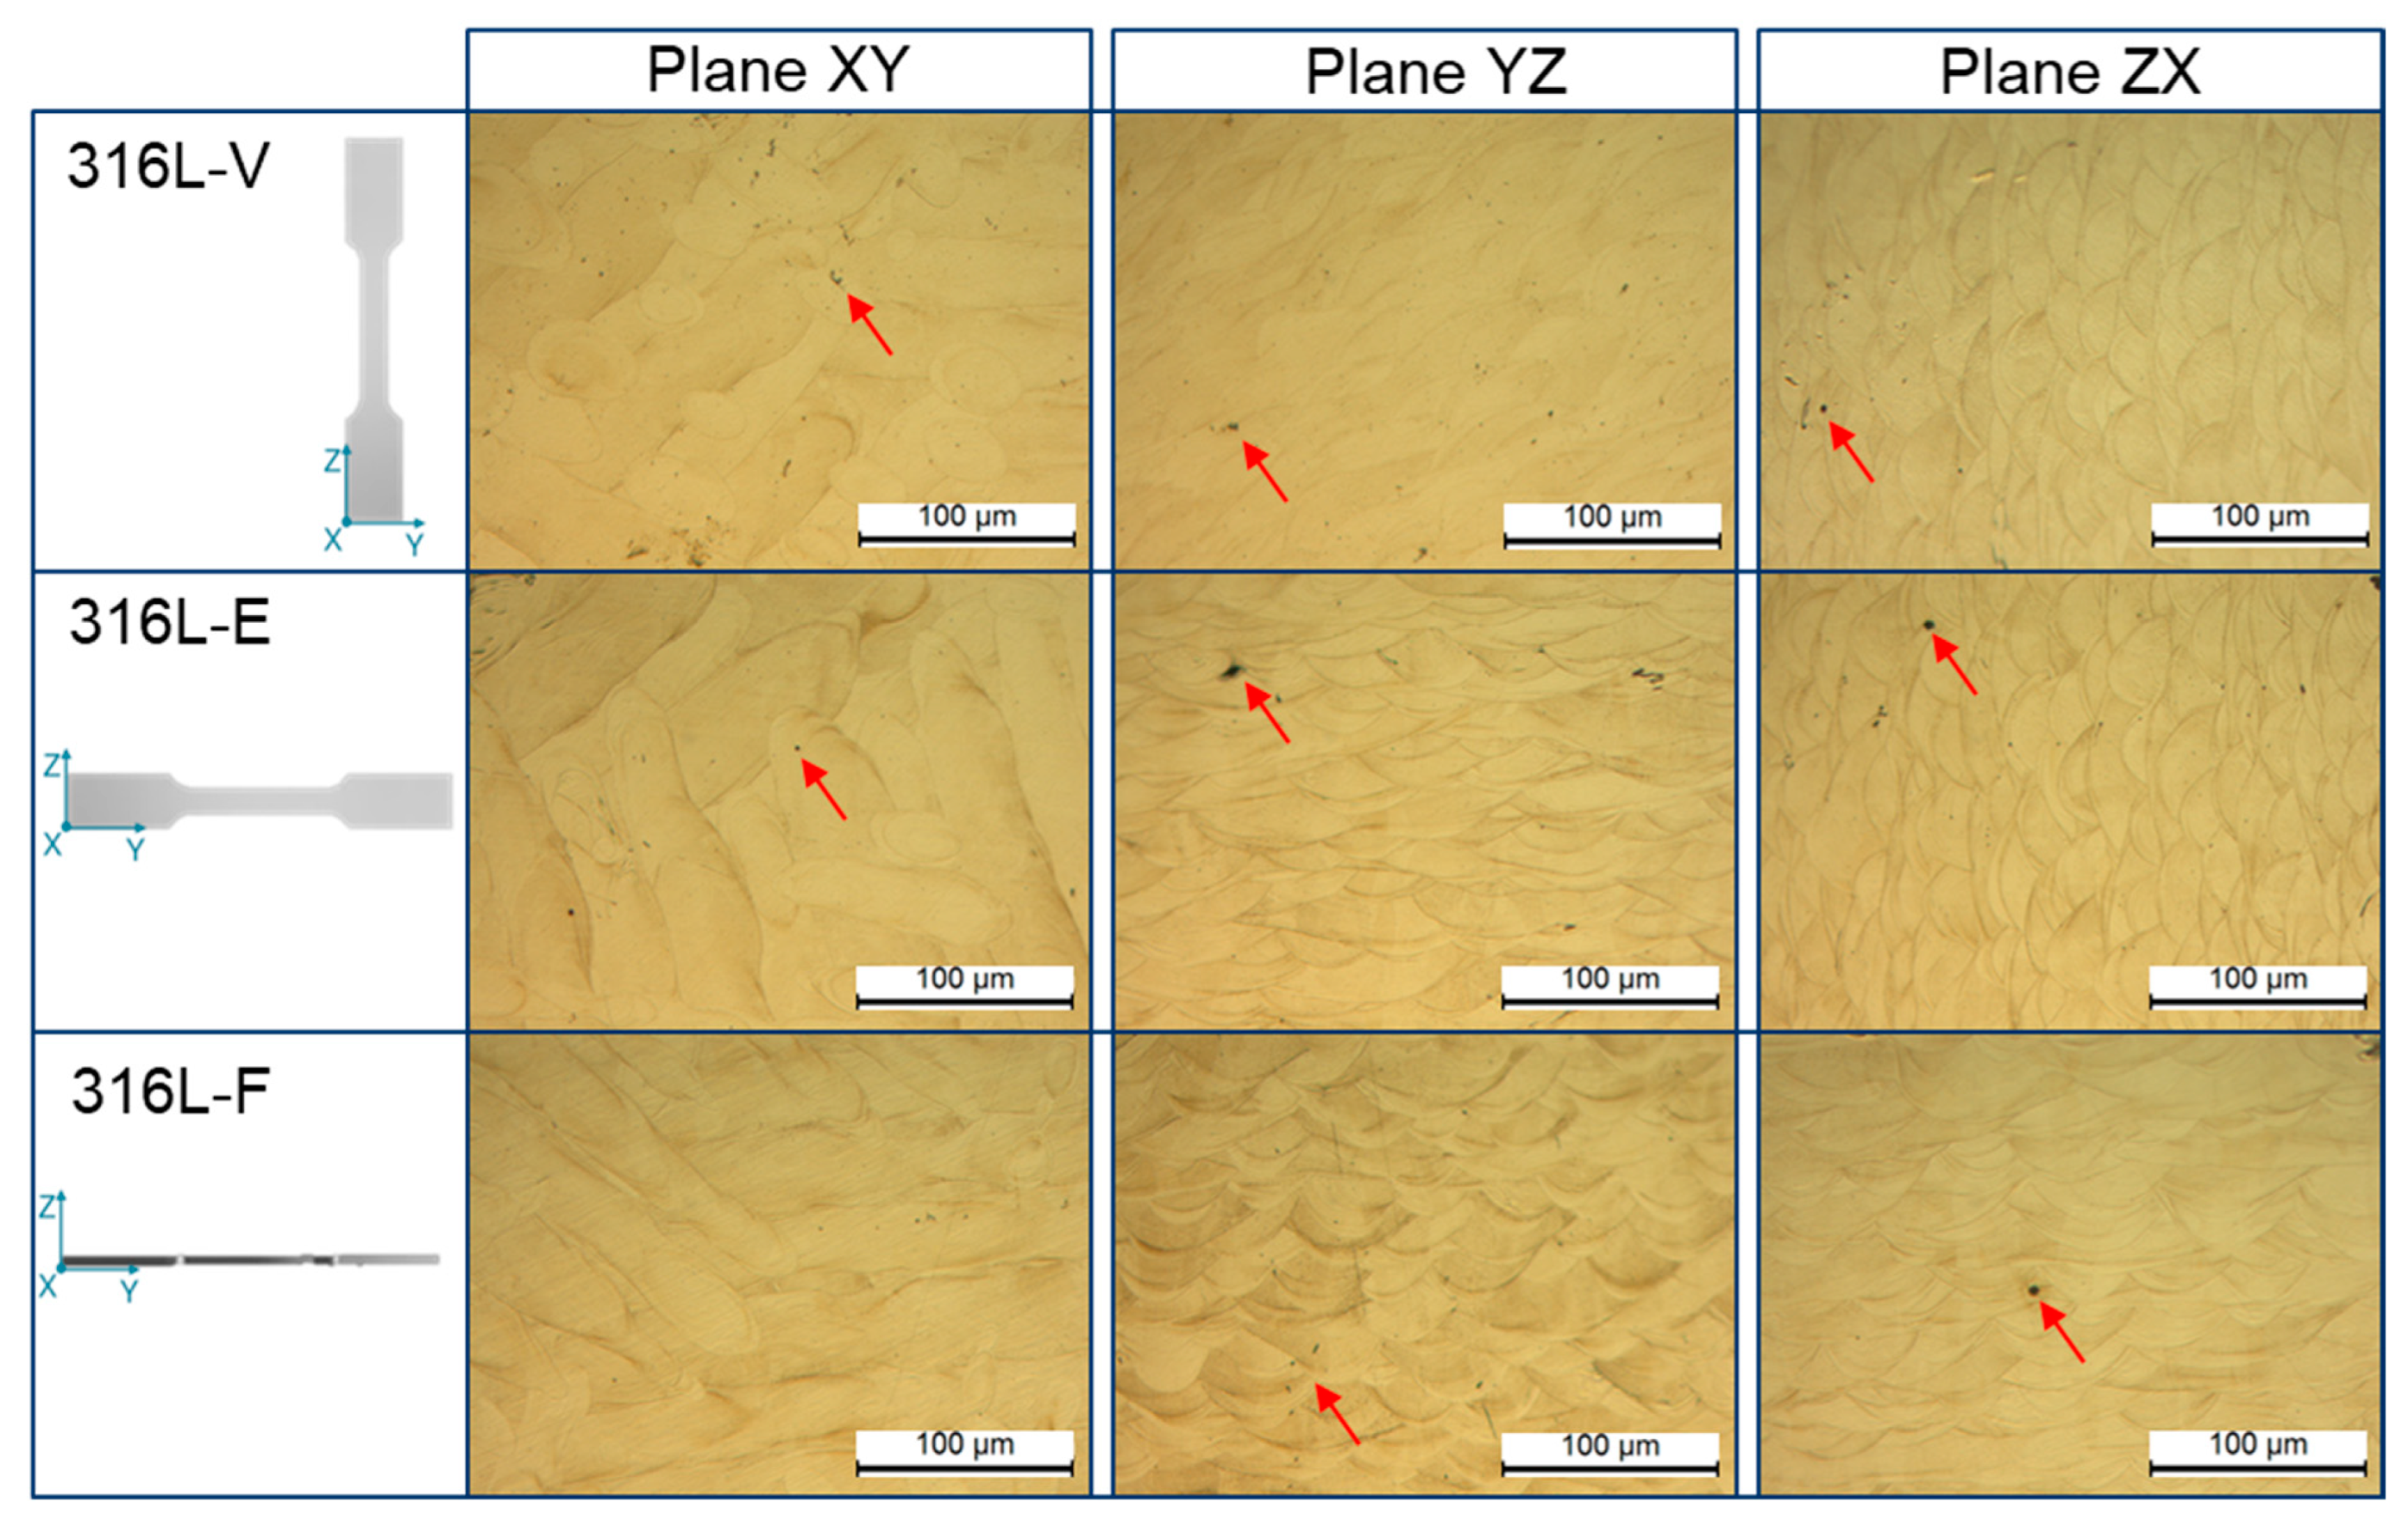
Figure 2 shows the microstructure of L-PBF 316L ss according to its building orientation. Plane XY reveals the laser tracks from the L-PBF process, and planes YZ and ZX show a network of melt pools in each layer, like welding beads, formed due to the overlap of the laser-scanning patterns. These melt pools have ~50 and ~150 μm depth and width, respectively. Figure 2 also reveals a high densification of the samples, with a residual porosity content (marked with red arrows in Figure 2) lower than 1%, regardless of building orientation. This value was obtained through LAS.V4 Leica image analysis software.
Figure 2.
Cross-sectional characterisation by optical microscopy of the as-built L-PBF 316L ss based on the building orientation: 316-V, 316L-E, and 316L-F samples.
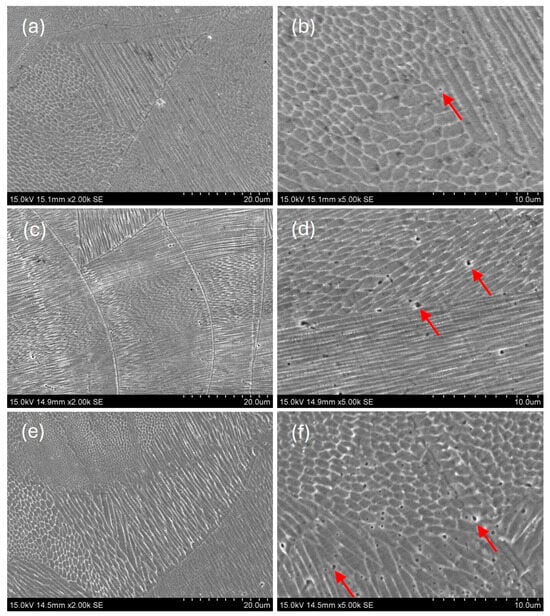
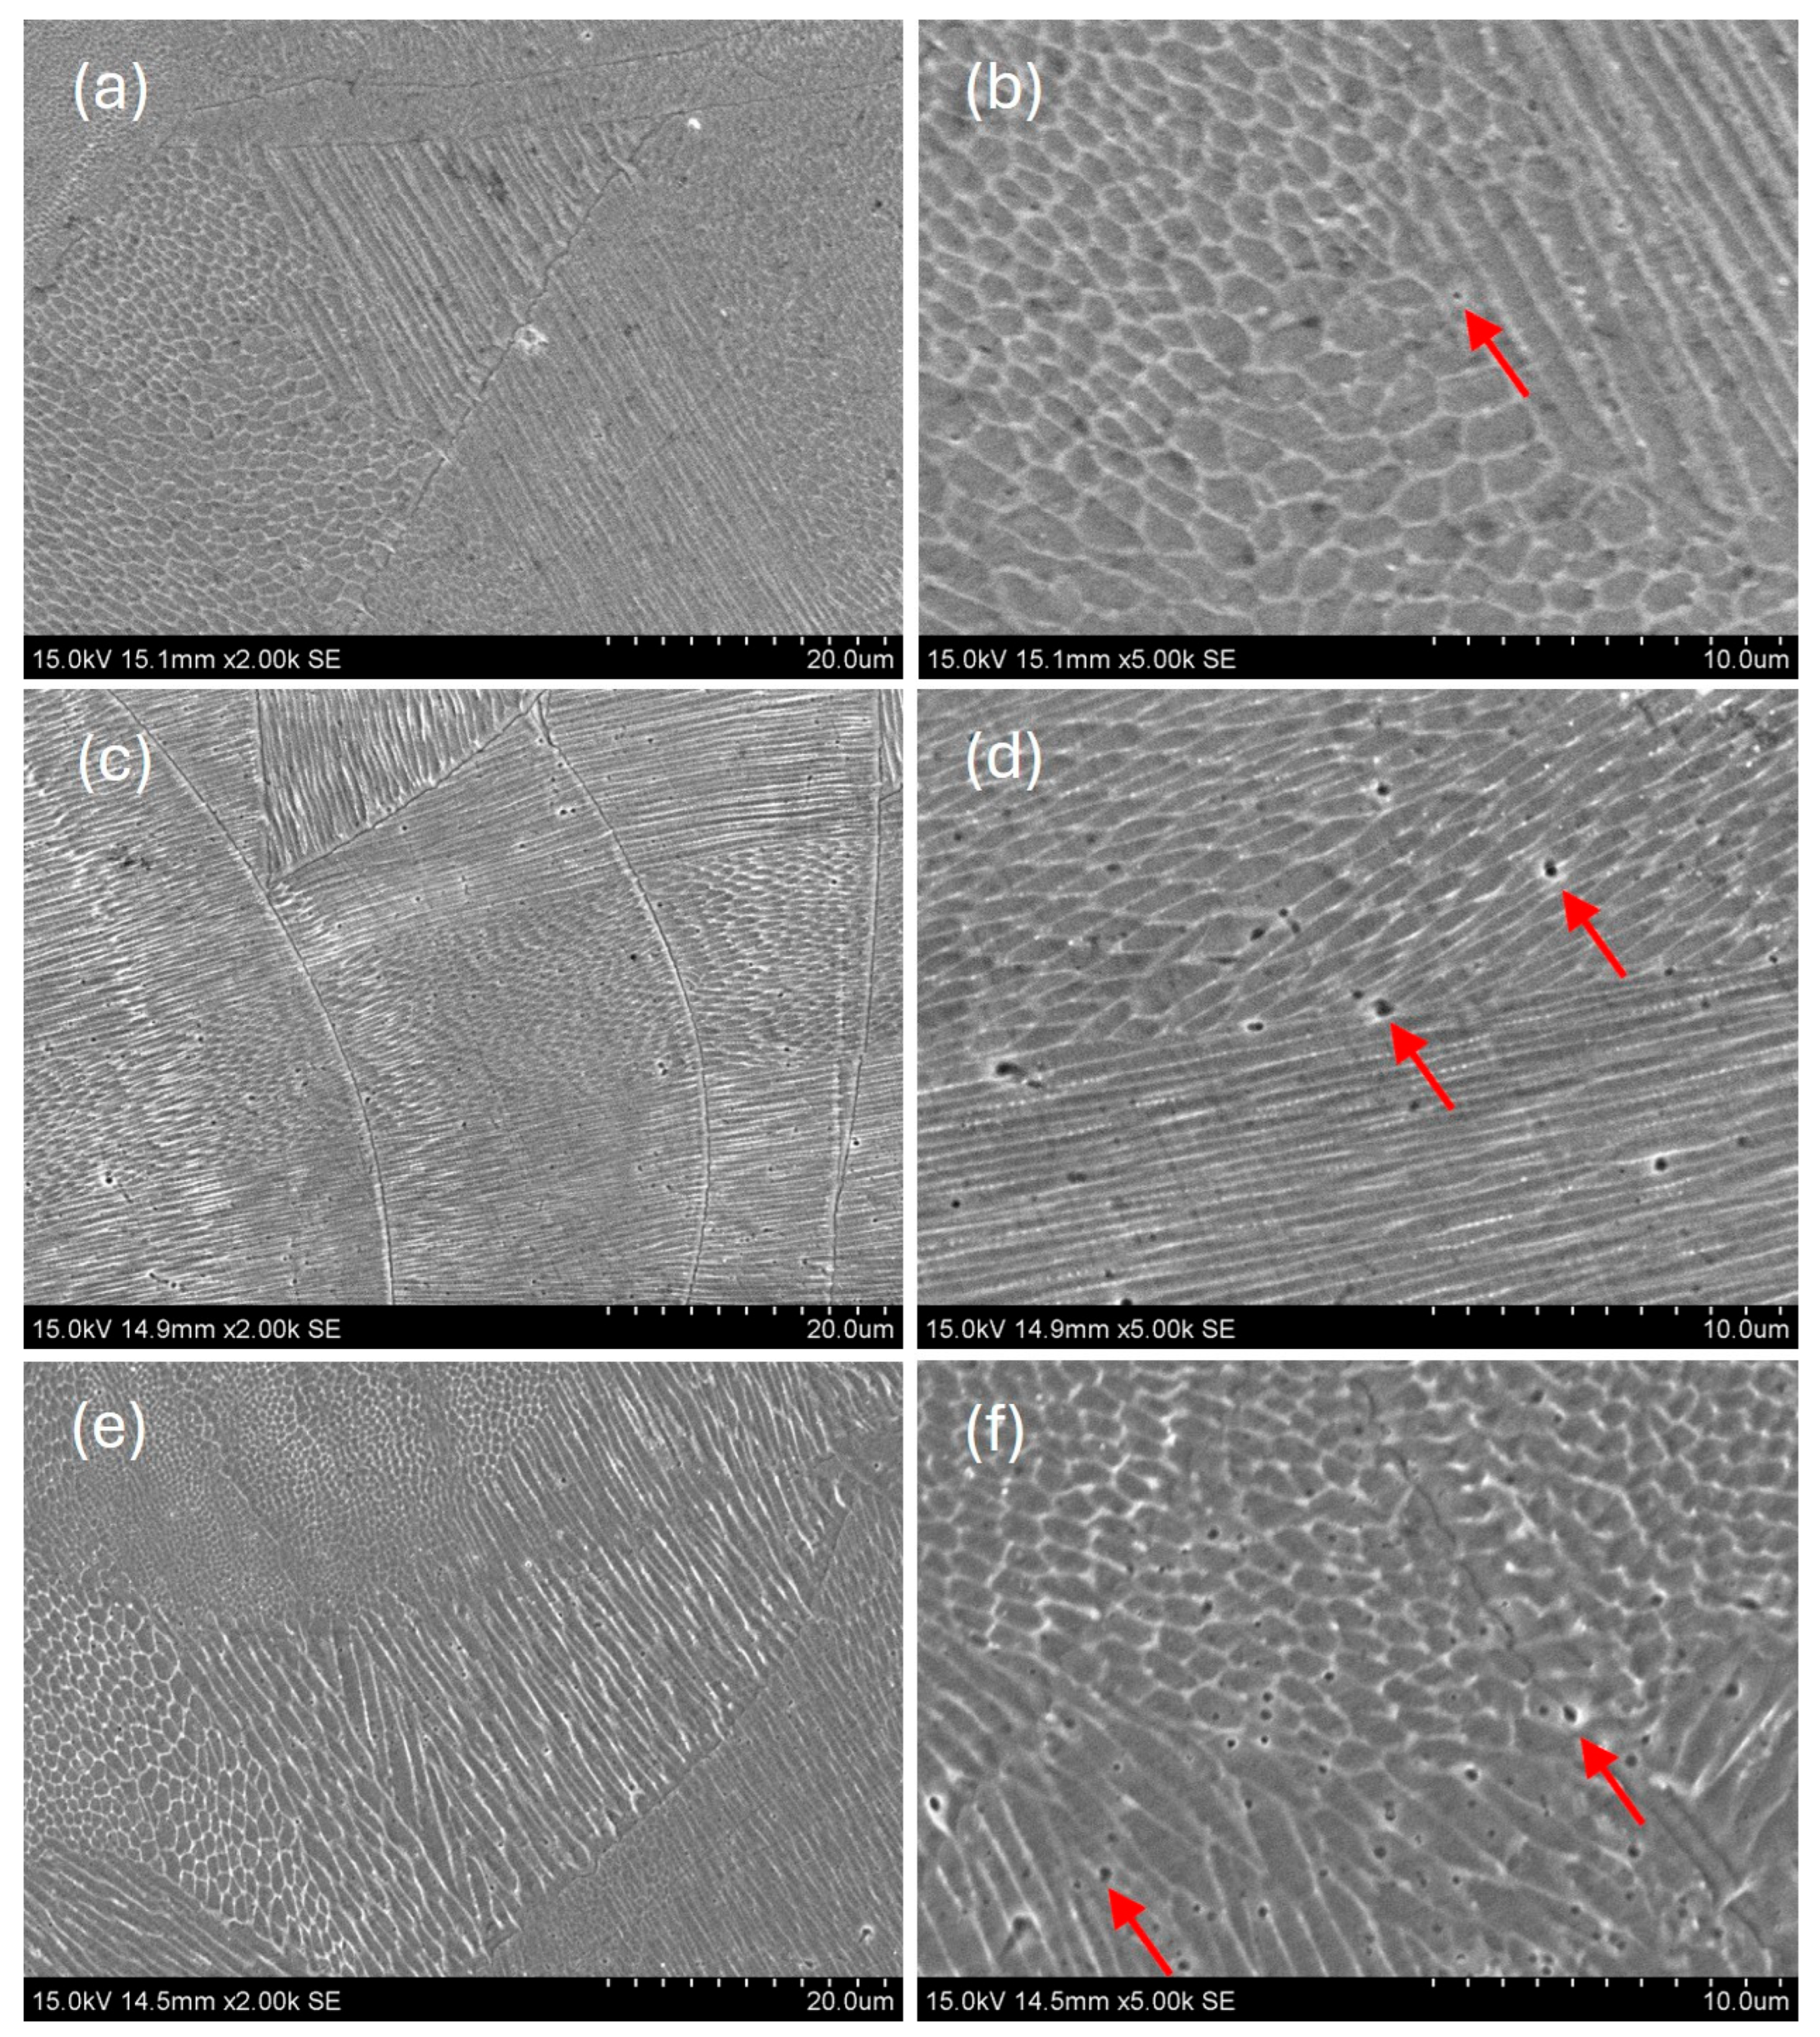
The SEM micrographs of Figure 3 reveal, at higher magnifications, the complex cellular microstructure and the fine sub-grains characteristic of the L-PBF process. The elongated cells are below two microns in width and some microns in length. This cellular microstructure is produced because of the high cooling rate and the large degree of undercooling associated with rapid quenching of the stainless steel due to the localised laser melting. In addition, the microstructure is fully austenitic, as expected for 316L stainless steel processed under these conditions, and no ferrite phase was detected. This is typical for 316L alloys with low carbon content and high nickel concentration, which stabilise the austenitic phase and provide excellent corrosion resistance and ductility. The L-PBF process has an estimated cooling rate of 103–108 K/s [40]. The content of sub-pores (red arrows marked in Figure 3) is low, and the building orientation does not have relevant effects on the complex cellular microstructure, as can be seen comparing Figure 3a–f.
Figure 3.
Cross-sectional SEM microstructure of the as-built L-PBF 316L ss based on building orientation: (a,b) 316L-V, (c,d) 316L-E, and (e,f) 316L-F samples at ×2000 and ×5000 magnification.
3.2. Surface Characterisation of the Corroded Samples
The samples were exposed to the three aggressive environments after the microstructural characterisation of the as-built material and before tensile tests. For the analysis of the corrosion mechanisms and damage suffered by the 316L ss in these environments, the samples built in the vertical orientation were used as reference: 316L-V-H2SO4, 316L-V-NaCl, and 316L-V-O.
3.2.1. H2SO4 Water Solution
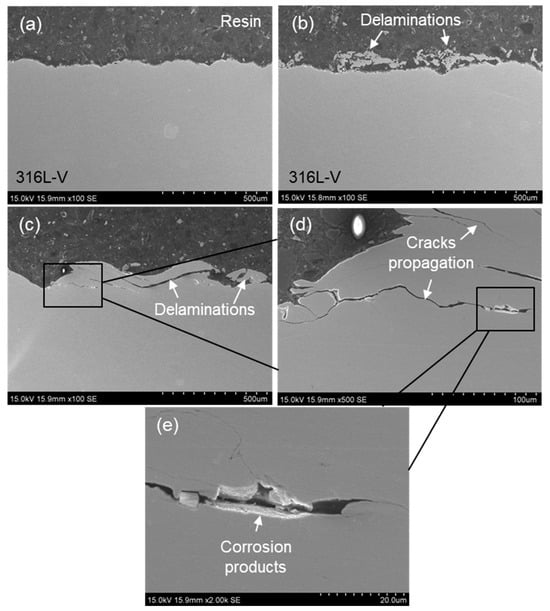
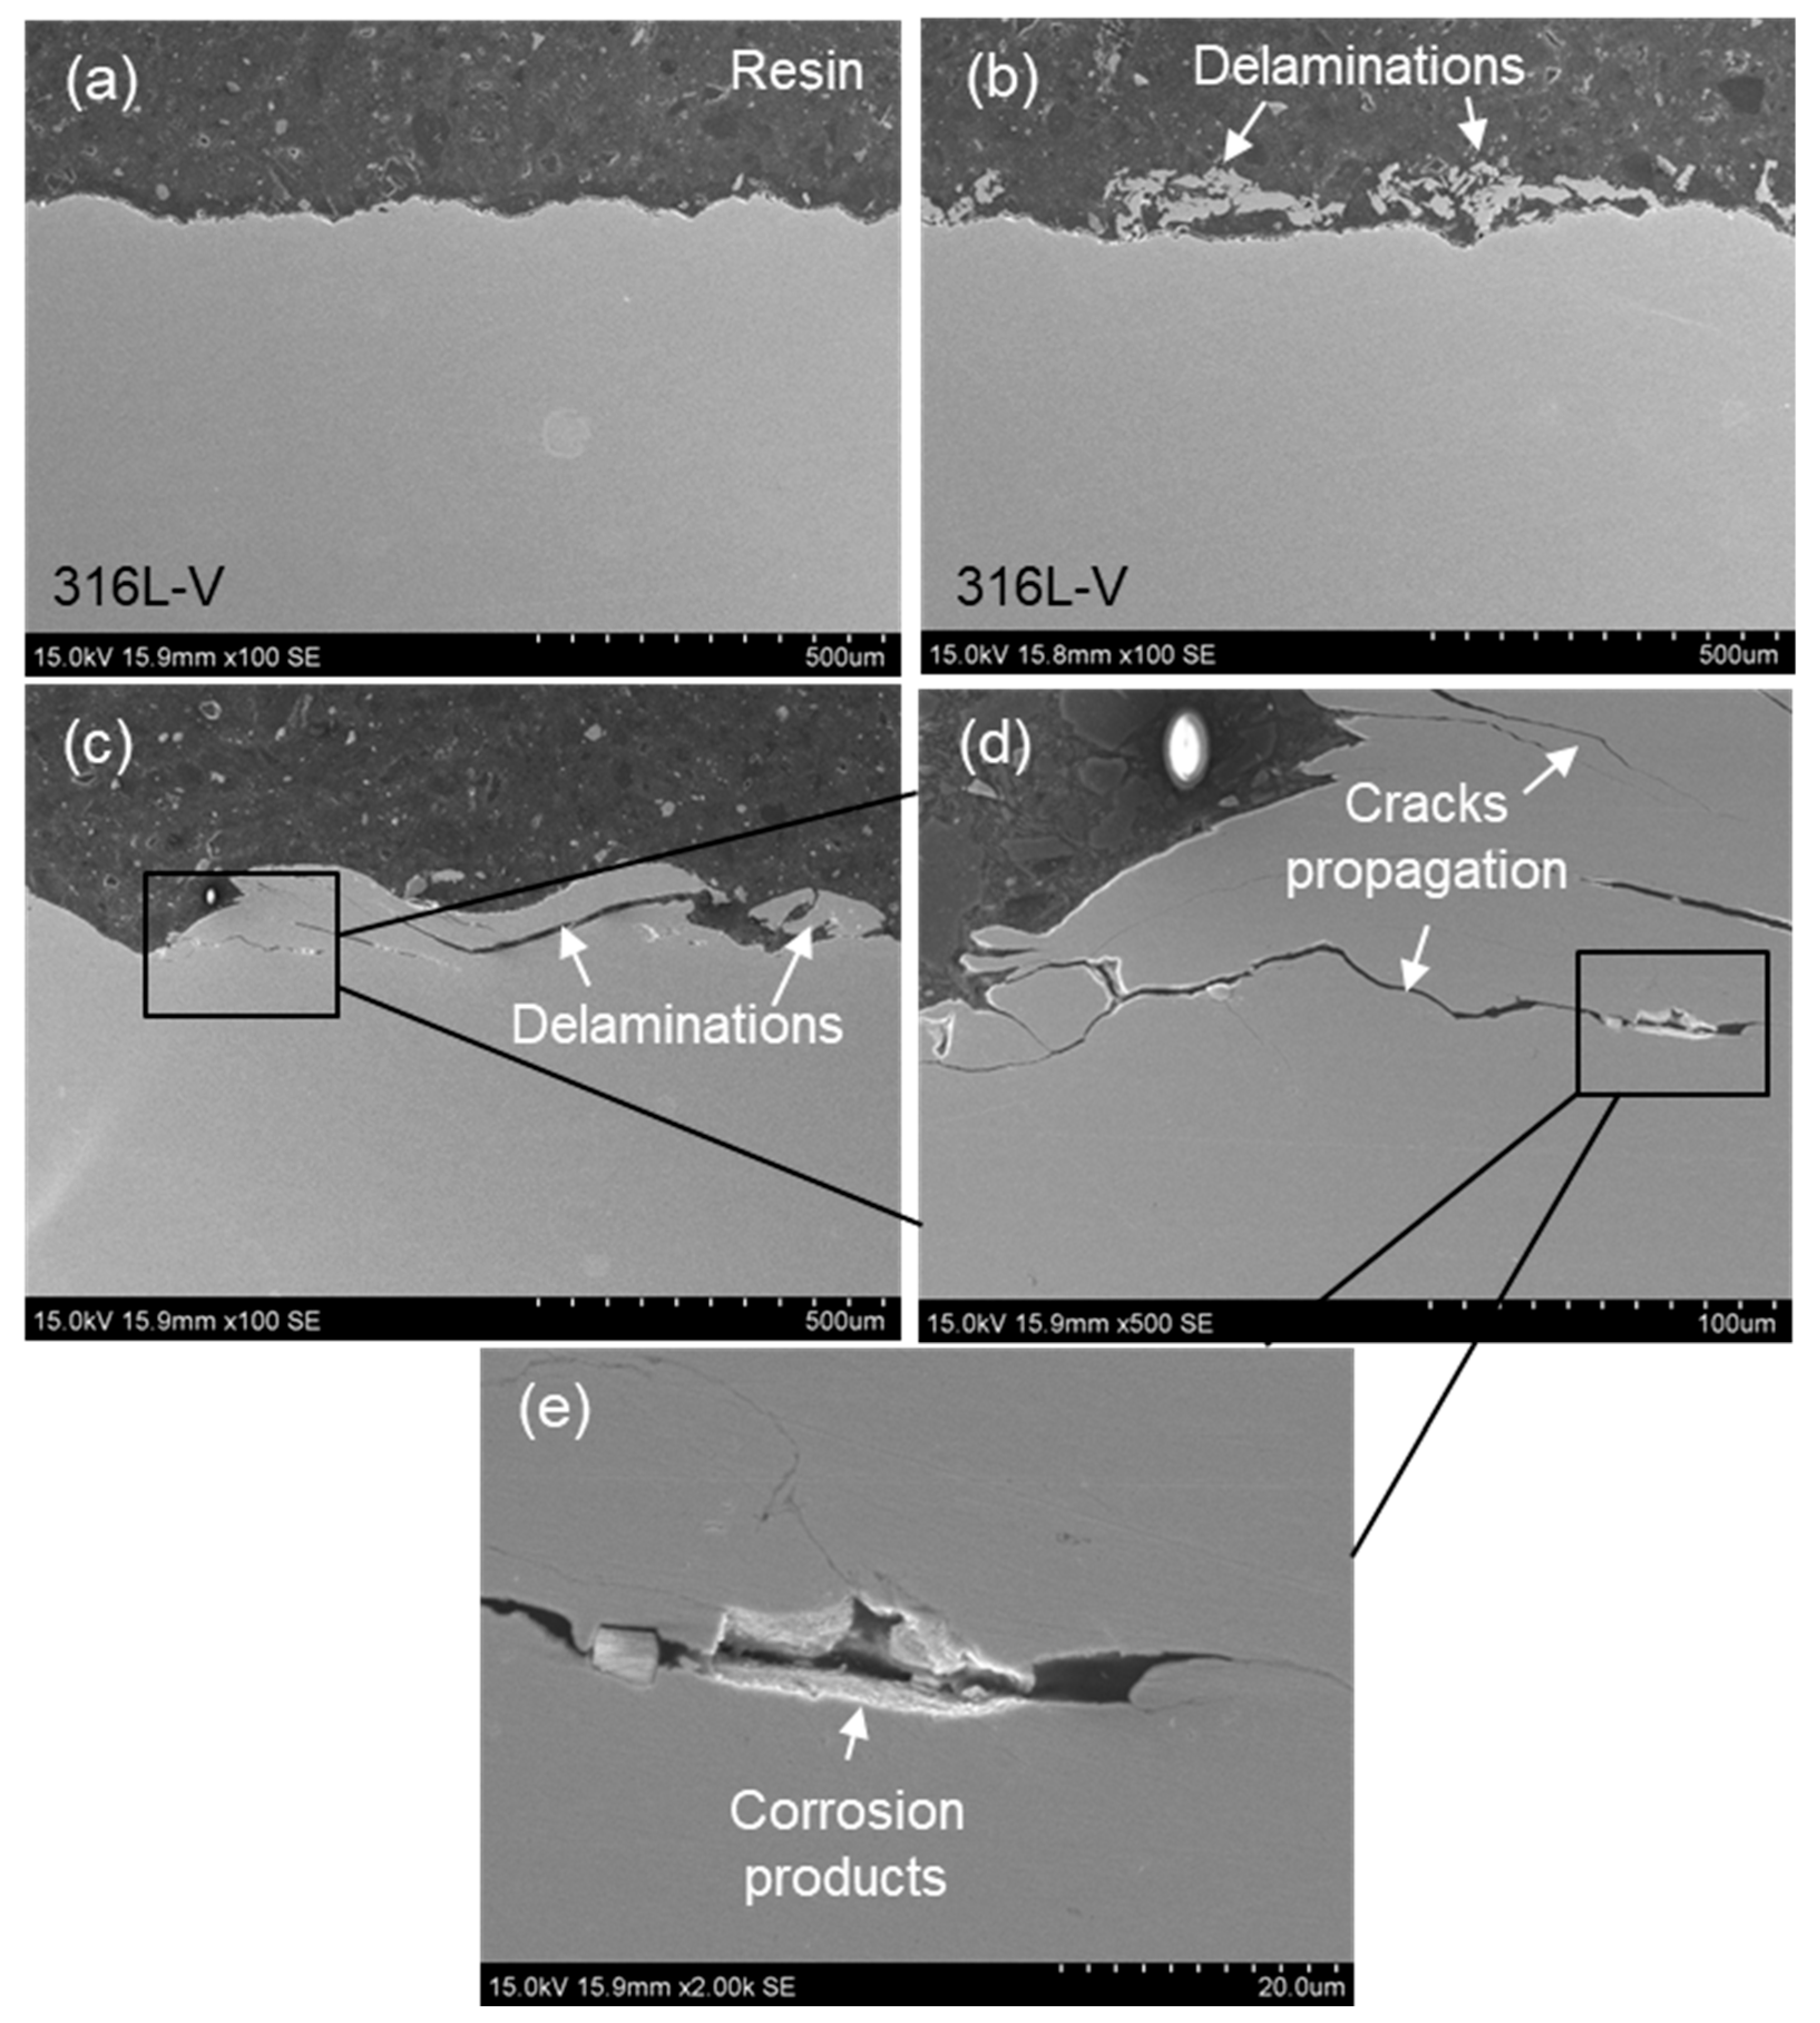
Figure 4 shows the cross-sectional SEM characterisation of the 316L-V-H2SO4 sample after its exposure to the 1 M H2SO4 water solution for 360 h. Figure 4a–c show an overview of the cross-section of the sample surface at ×100 magnification in different areas, and as can be seen in Figure 4a, no damage has been observed in some of them. In contrast, other areas suffered material spallation and delamination, as shown in Figure 4b,c. The SEM image at higher magnification (×500) of Figure 4d shows how material delamination is produced by the formation and posterior propagation of cracks near the surface. Finally, Figure 4e, a detail at a higher magnification (×2000) from Figure 4d, shows the deposition of corrosion products at the end of the crack that led to its propagation. According to Guzmán-Nogales et al. [41], these products generate a more significant dissolution of the passive layer formed by the 316L ss. The presence of sulphate ions (SO4−), together with the acidic pH of the electrolyte, developed the corrosion process, forming cracks after the breakdown of the Cr2O3 passive layer [42]. The formation of these cracks is also a consequence of the embrittlement of the alloy in contact with the acidic electrolyte. However, 360 h of exposure to this aggressive environment was not enough to identify signs of damage in the inner areas of the sample, because the identified cracks only affect the most superficial part of the samples, reaching depths of less than ~200 µm.
Figure 4.
Cross-sectional SEM characterisation of L-PBF 316L ss exposed to 1 M H2SO4 solution for 360 h at different magnifications: (a–c) ×100, (d) ×500, and (e) ×2000.
3.2.2. NaCl Water Solution
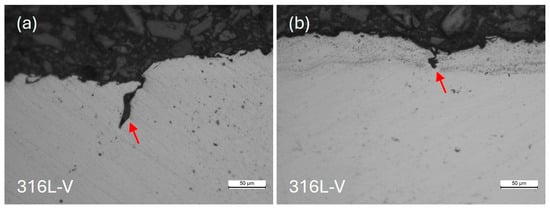
Figure 5 shows the cross-section of the L-PBF 316L-V-NaCl sample after its immersion in the 3.5 wt.% NaCl water solution for 360 h in two different areas. Some isolated pits identified in the cross-section of the sample indicate the beginning of the pitting corrosion mechanism. These pits, red arrows marked in Figure 5a,b, have a few microns in diameter but several tens of microns in depth. Their formation is caused by the localised attack produced by Cl− ions, mainly in the sub-grains of the microstructure and the pores [25,41]. The 316L-NaCl samples did not suffer from delamination, and no evidence of spallation was observed.
Figure 5.
Cross-sectional characterisation by OM of the L-PBF 316L ss exposed to the 3.5 wt.% NaCl solution for 360 h in two different regions: (a) ×100 and (b) ×100.
3.2.3. High-Temperature Oxidation
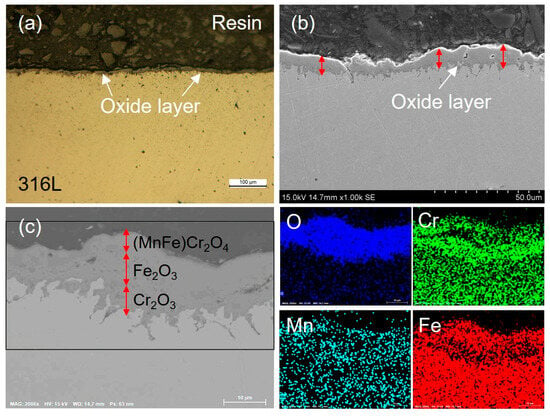
Figure 6 shows the cross-sectional micrographs of the 316L-V-O sample after 360 h exposed at 800 °C. Figure 6a shows the formation of a continuous layer of oxides along the surface, and Figure 6b shows details of this oxide layer. It has ~10 µm thickness (red arrows marked in Figure 6b) and is well adhered to the surface, as the substrate-coating interface shows at higher magnification in Figure 6c, providing protection capacity to the stainless steel. The EDX analysis, also shown in Figure 6c, reveals that this oxide layer is formed mainly by Cr and Fe-rich oxides. The composition of the coating shows three different layers. It is consistent with the following structure: chromia (Cr2O3) at the bottom, hematite (Fe2O3) in the middle zone of the coating, and spinel oxides, mainly (MnFe)Cr2O4, at the top of the coating. This phase configuration has been studied in detail in previous works and confirmed by X-ray diffraction [31]. No relevant morphological or compositional differences have been observed in the oxide layer of 316L-V-O, 316L-E-O, and 316L-F-O samples, suggesting that the oxidation process is not highly influenced by building orientation.
Figure 6.
Cross-sectional characterisation by OM and SEM of the L-PBF 316L ss exposed to high temperature (800 °C) for 360 h at different magnifications: (a) ×200, (b) ×1000, and (c) EDX analysis at ×2000.
3.3. Microstructural Analysis of the Corroded Samples
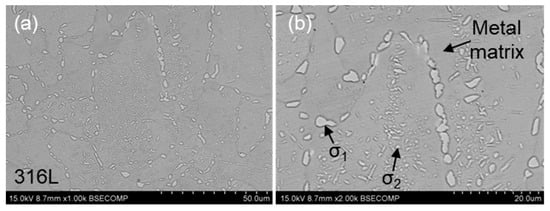
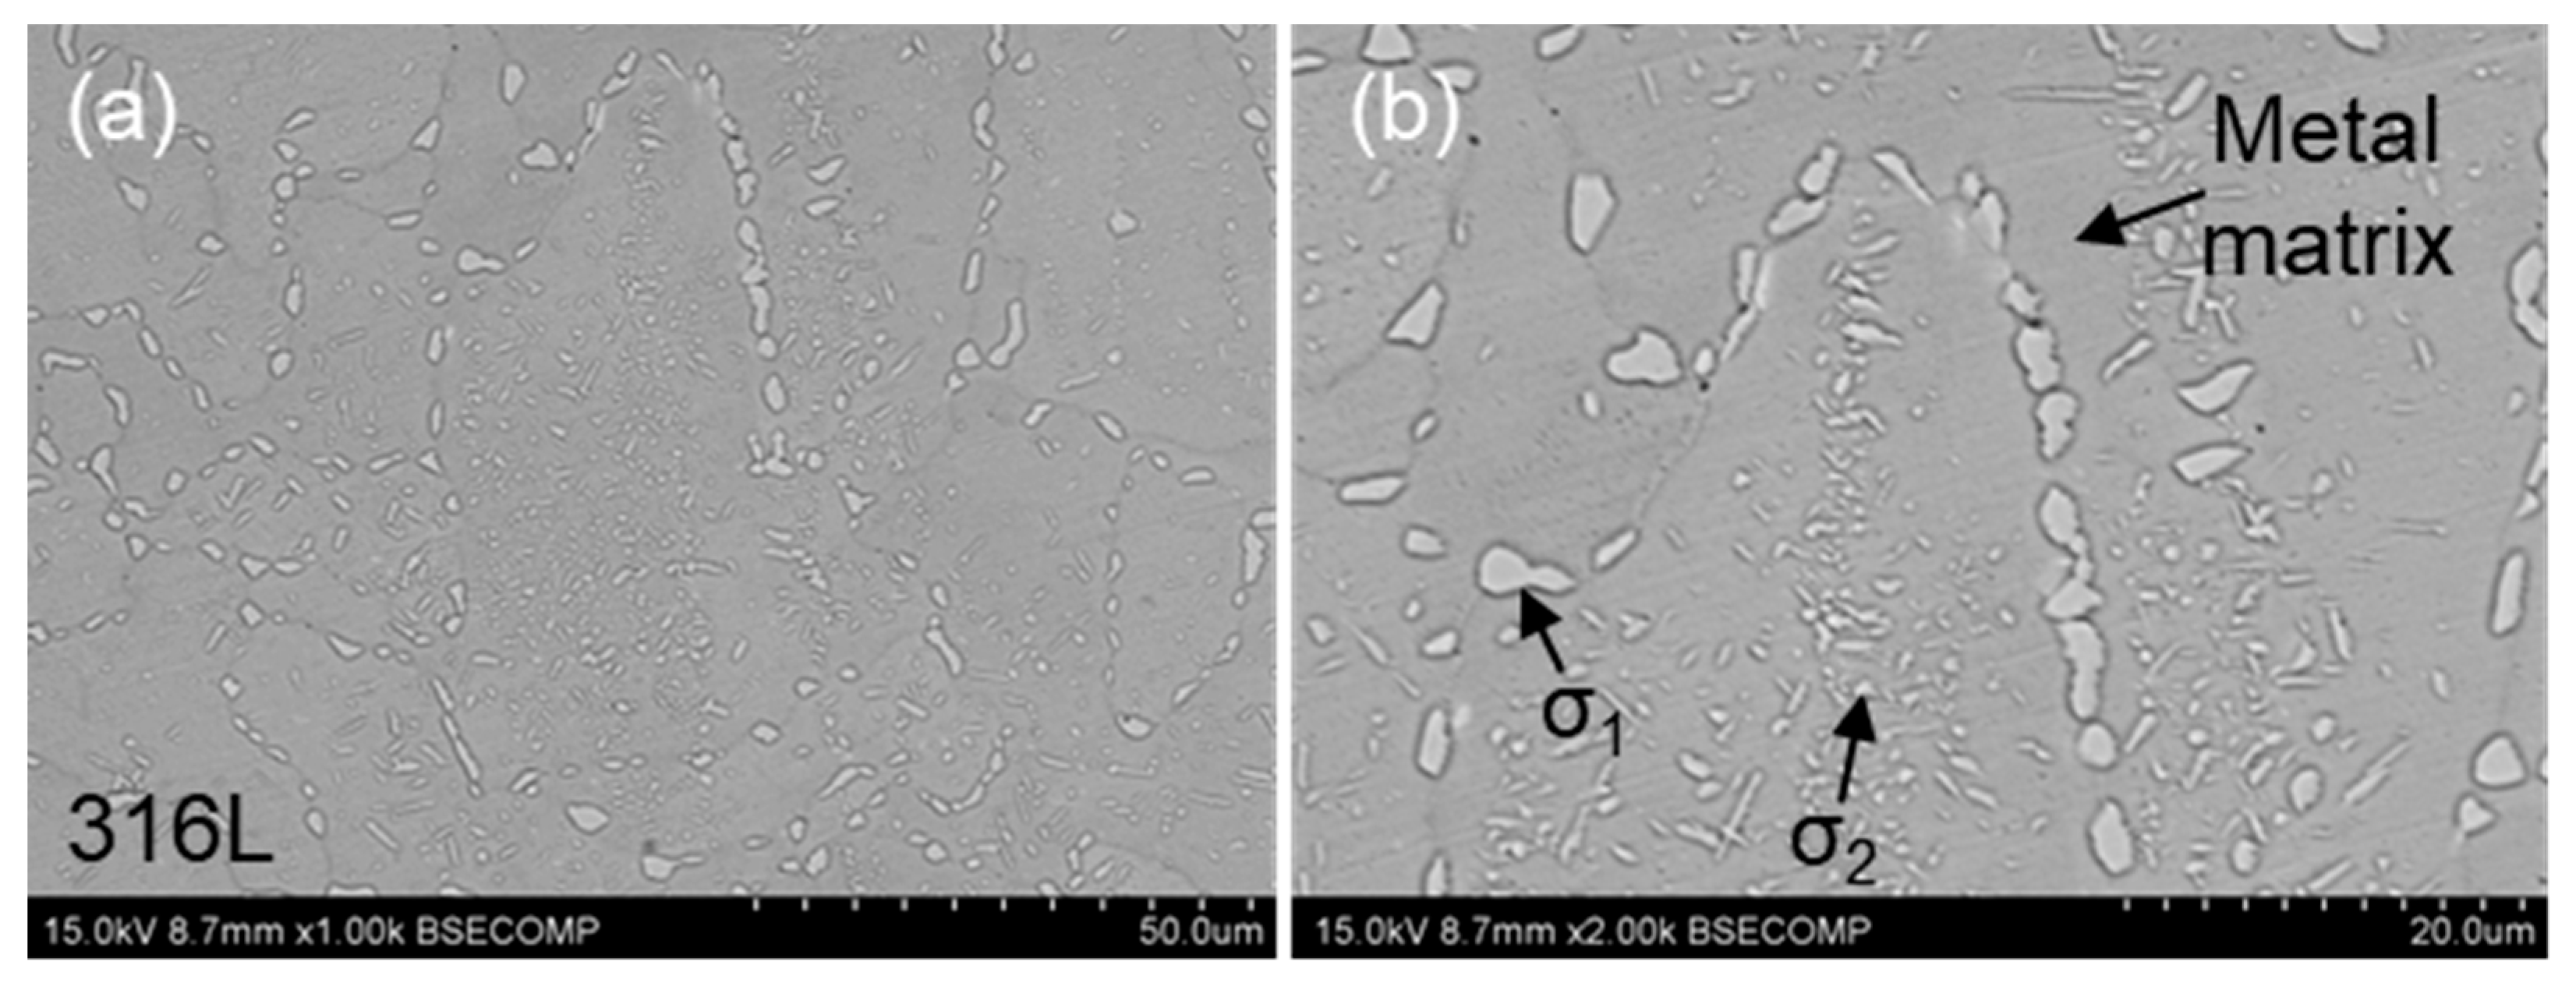
316L-H2SO4 and 316L-NaCl samples did not undergo any microstructural modifications compared to the as-built 316L ss, and the exposure to these environments only produced changes in their surface. However, the 316L-O sample exhibits important changes in its microstructure compared to the as-built 316L ss, as Figure 7 shows. The long exposure period at 800 °C eliminated the complex cellular microstructure found in Figure 3 and the fine sub-grains characteristic of the L-PBF process (Figure 7a). The new precipitates, as marked by the arrows in Figure 7b, were identified by Houshang et al. as σ phase [43]. The growth of the σ phase precipitates in L-PBF 316L ss is primarily controlled by particle growth at the early stage and particle coarsening (primarily through Ostwald ripening) at the later stage. This phase has the typical chemical form of (Fe,Ni)x(Cr,Mo)y and was identified in two different regions. On the one hand, the σ phase forms in the grain boundaries of the new grains, and it has a rounded shape with a size of ~3 µm. This phase has been identified as σ1 in Figure 7b. On the other hand, the σ phase also grows within the interior of the new grains, exhibiting a needle shape and smaller size (~0.3 and ~3 µm in width and depth, respectively); in this case, it has been identified as σ2 in Figure 7b. The punctual EDX analysis performed revealed the same composition on both σ phases and the presence of 52 ± 3 Fe, 28 ± 2 Cr, 12 ± 2 Mo, 7 ± 1 Ni, and 1 ± 1 Si (in wt.%), following the average composition reported by other authors: 44–59 Fe, 29 Cr, 8–11 Mo, and 5 Ni (in wt.%) [44,45]. In contrast, the elemental composition of the metal matrix has lower contents of Cr and, particularly, Mo, and it is 63 ± 2 Fe, 19 ± 1 Cr, 14 ± 1 Ni, 3 ± 1 Mo and 1 ± 1 Si (in wt.%). It is important to note that EDS provides semi-quantitative results and can be affected by matrix effects and interaction volume, which may explain the slightly higher Ni content compared to typical σ-phase values reported in the literature. Nevertheless, the observed enrichment in Cr and Mo, together with the morphology and location of the precipitates, strongly supports their identification as σ-phase.
Figure 7.
Microstructural characterisation by SEM of the 316L ss after high-temperature oxidation at 800 °C in a dry air atmosphere for 360 h at different magnifications: (a) ×1000, and (b) ×2000.
3.4. Tensile Tests
3.4.1. Effect of Building Orientation
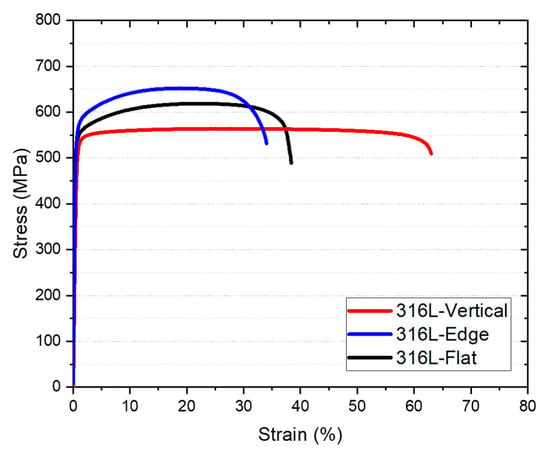
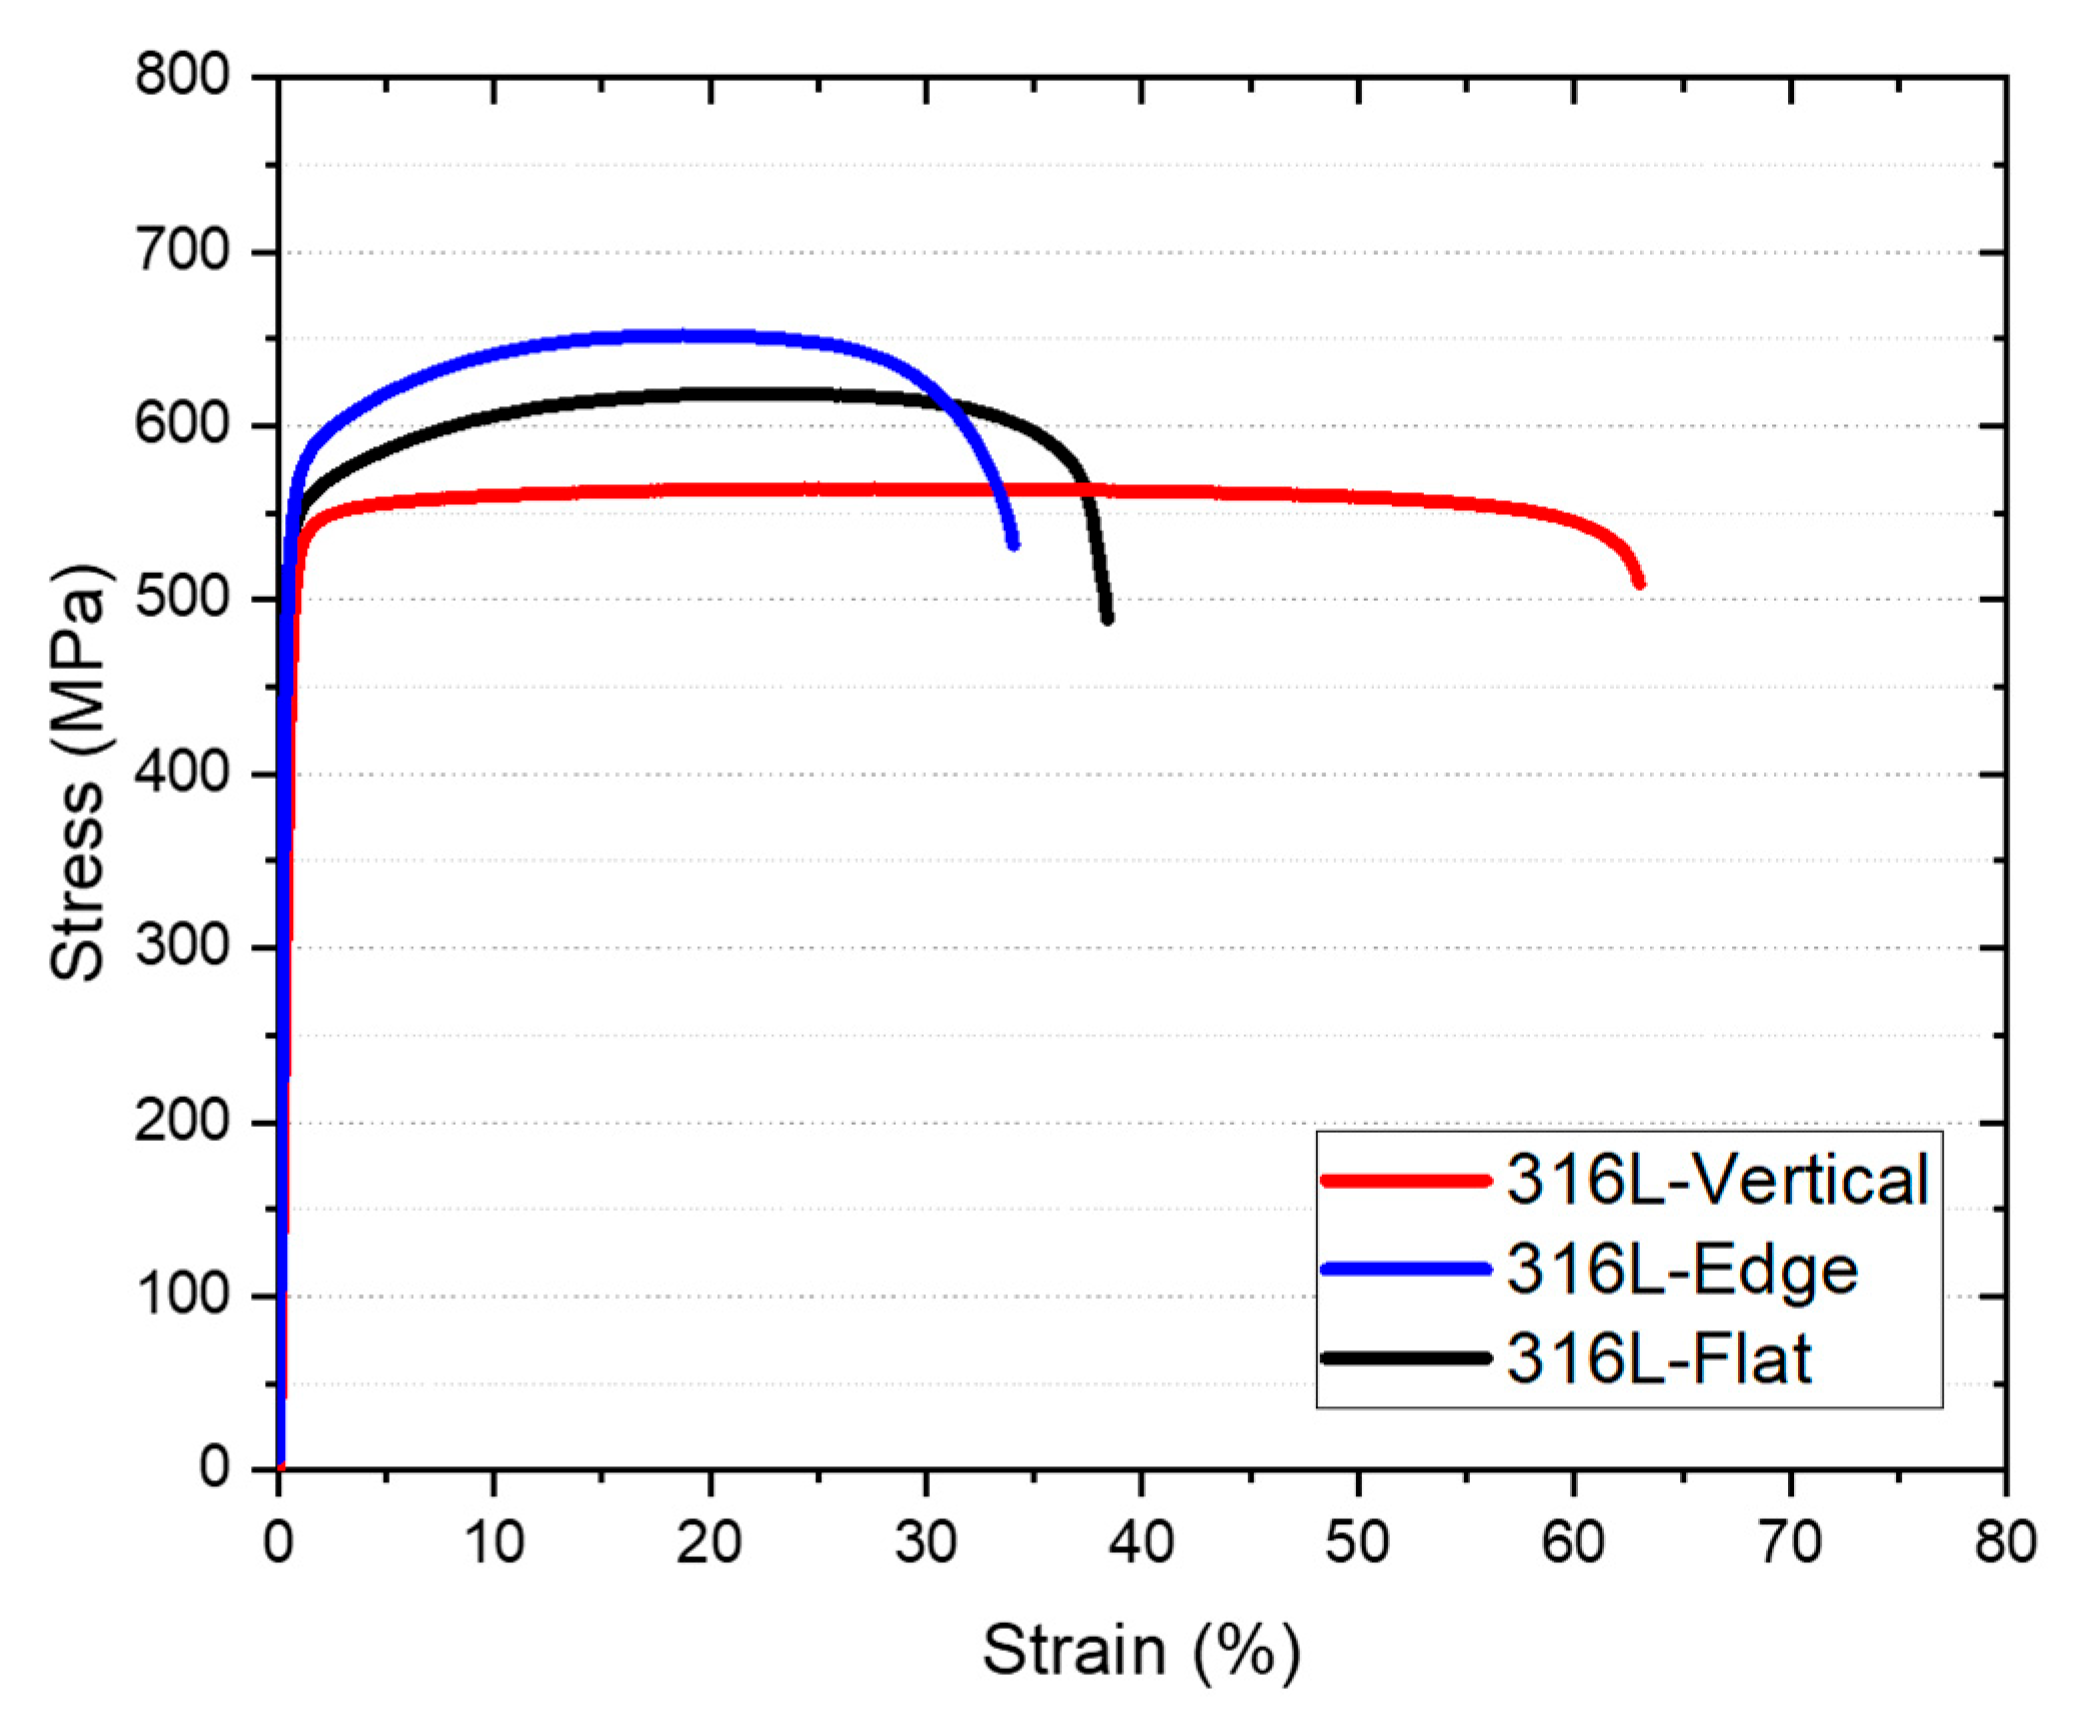
Figure 8 shows the representative engineering stress–strain curves of the as-built L-PBF 316L ss according to the building orientation. This parameter significantly affects the mechanical properties. In this context, 316L-E and 316L-F samples have superior tensile strength to 316L-V samples. They increased tensile strength by ~16% and ~10%, respectively, compared to the 316L-V sample, but they also increased yield strength by ~6% and ~4%, respectively, as Table 3 shows. These results follow those of Casati et al. [46]. This behaviour is due to the concentration of microsegregations, oxides, inclusions, lack of fusion, and porosity at the borders between melt pools in the L-PBF pieces. This heterogeneous distribution of defects reduces the mechanical properties of the 316L-V sample, where the effect of these borders is higher due to their orientation with respect to the direction of the applied stress. However, the 316L-V sample increased strain by ~80% and ~68%, compared to the 316L-E and 316L-F samples. This is because the epitaxial grains characteristic of L-PBF microstructures grown in the heat dissipation direction [47] are parallel to the applied stress direction for 316L-V and perpendicular for 316L-E and 316L-F samples. These columnar epitaxial grains promote higher ductility in the 316L-V pieces by coinciding their orientation with the direction of the applied stress. For these reasons, manufacturing in the vertical orientation produces much more significant mechanical differences in the piece than in the flat and edge orientations, where the differences in the mechanical properties are much more minor.
Figure 8.
Representative engineering stress–strain curves of the L-PBF 316L ss based on building orientation: vertical, edge, and flat.
Table 3.
Average results of the tensile strength (in MPa), yield strength (in MPa), and strain (in %) of the L-PBF 316L ss based on building orientation.
The 316L-E and 316L-F samples exhibit superior tensile strength compared to the 316L steel obtained by conventional methods [48]. This is mainly attributed to the refinement in the microstructure of the alloy, which in turn is a result of the rapid solidification process that occurs during the L-PBF process [17]. Ductility values are superior to 35%, which is lower than conventional methods, but still high enough for most applications. In contrast, the 316L-V sample shows superior ductility with lower tensile strength than wrought steel. However, the yield strength is higher in the pieces manufactured by L-PBF, regardless of the manufacturing strategy, compared to the wrought pieces (Table 3). This design parameter justifies the great advantage of using the L-PBF technique for obtaining high mechanical performance steel samples, apart from the design freedom provided by the technique.
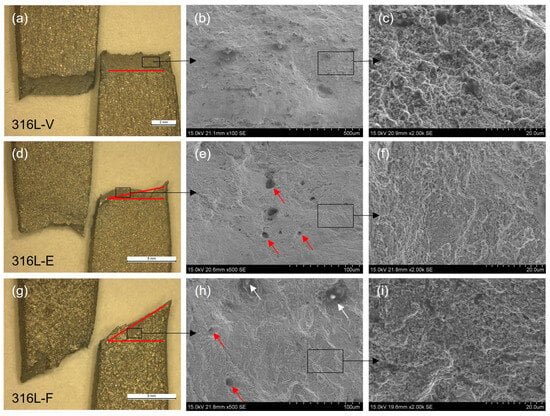
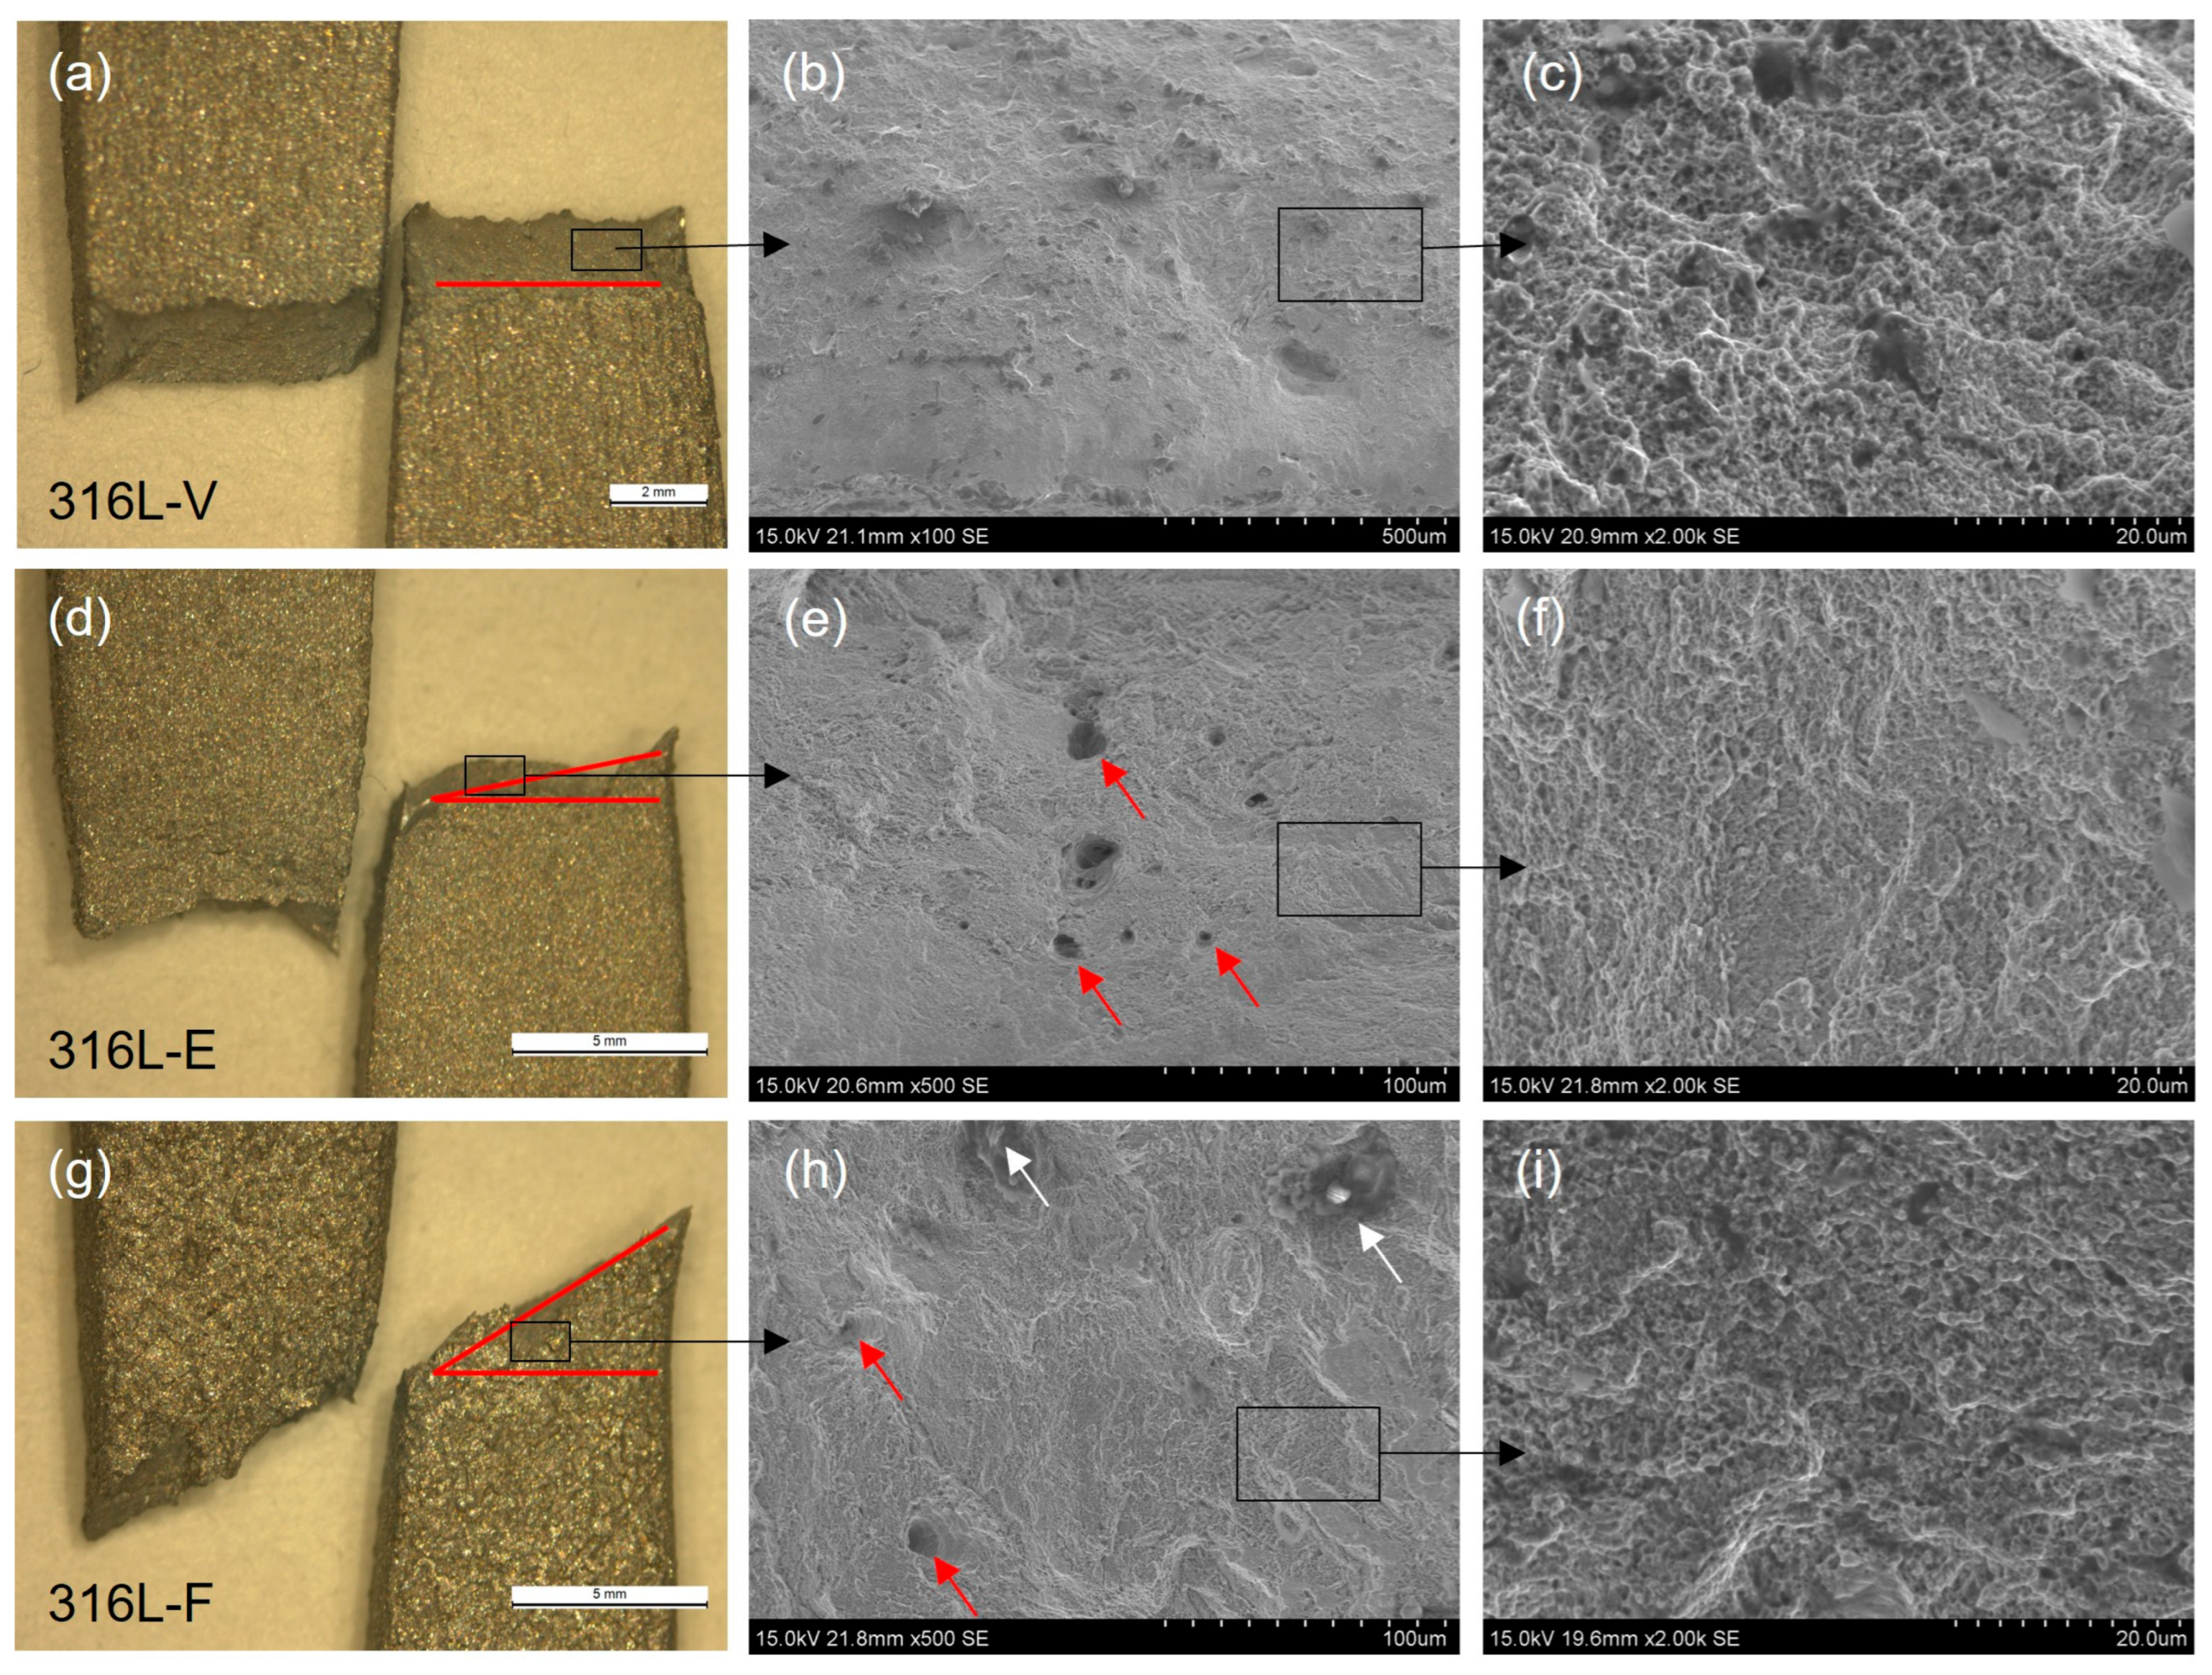
Figure 9 shows the fracture surface of the as-built 316L-V, 316L-E and 316L-F samples to investigate fracture mechanisms. The images obtained at low magnification for all the given conditions show the cup and cone morphology of the fractured pieces, which is characteristic of a ductile fracture. However, some relevant differences are shown in the fracture angle. 316L-V sample breaks perpendicular to the applied stress direction in the width direction but with an angle through the thickness, while 316L-E and 316L-F samples break with an angle through the thickness (Figure 9a,d,g, respectively). The SEM images at ×100 magnification of the three samples (Figure 9b,e,h) also show significant differences between the 316L-V sample and 316L-E and 316L-F samples. Crater-like voids on a scale of up to ~20 μm (red arrows marked in Figure 9e,h) were only shown in 316L-E and 316L-F samples, and they could act as the primary sites triggering fracture by causing cracks and accelerating crack propagation. Their presence explains the lower ductility in these samples compared with the 316L-V samples. In some areas, several partially melted particles were found on the fracture surface, as the white arrows of Figure 9h indicate. These are usually present at the interface between two layers and are a fundamental cause of premature fractures detected in samples exposed to tensile stress [46].
Figure 9.
Characterisation of the fracture surface of (a–c) 316L-V, (d–f) 316L-E, and (g–i) 316L-F after tensile strength tests.
Finally, the SEM images at ×2000 magnification (Figure 9c,f,i) show dimples in the fracture plane with a size like that of the cellular grains of L-PBF parts, characteristic also of the ductile fracture mechanism. However, it seems that these dimples are slightly higher on the surface of the 316L-V sample, which looks more deformed and explains the higher ductility reported in tensile tests.
3.4.2. Effect of the Aggressive Environment
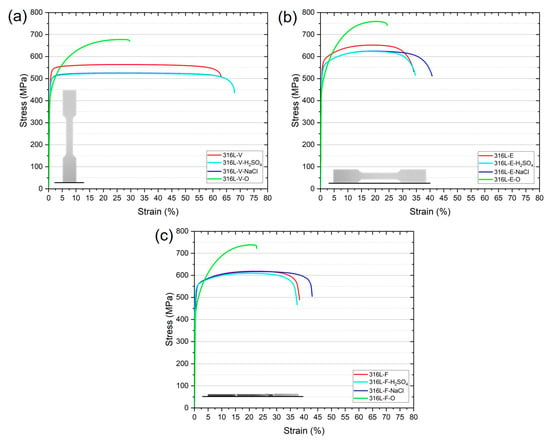
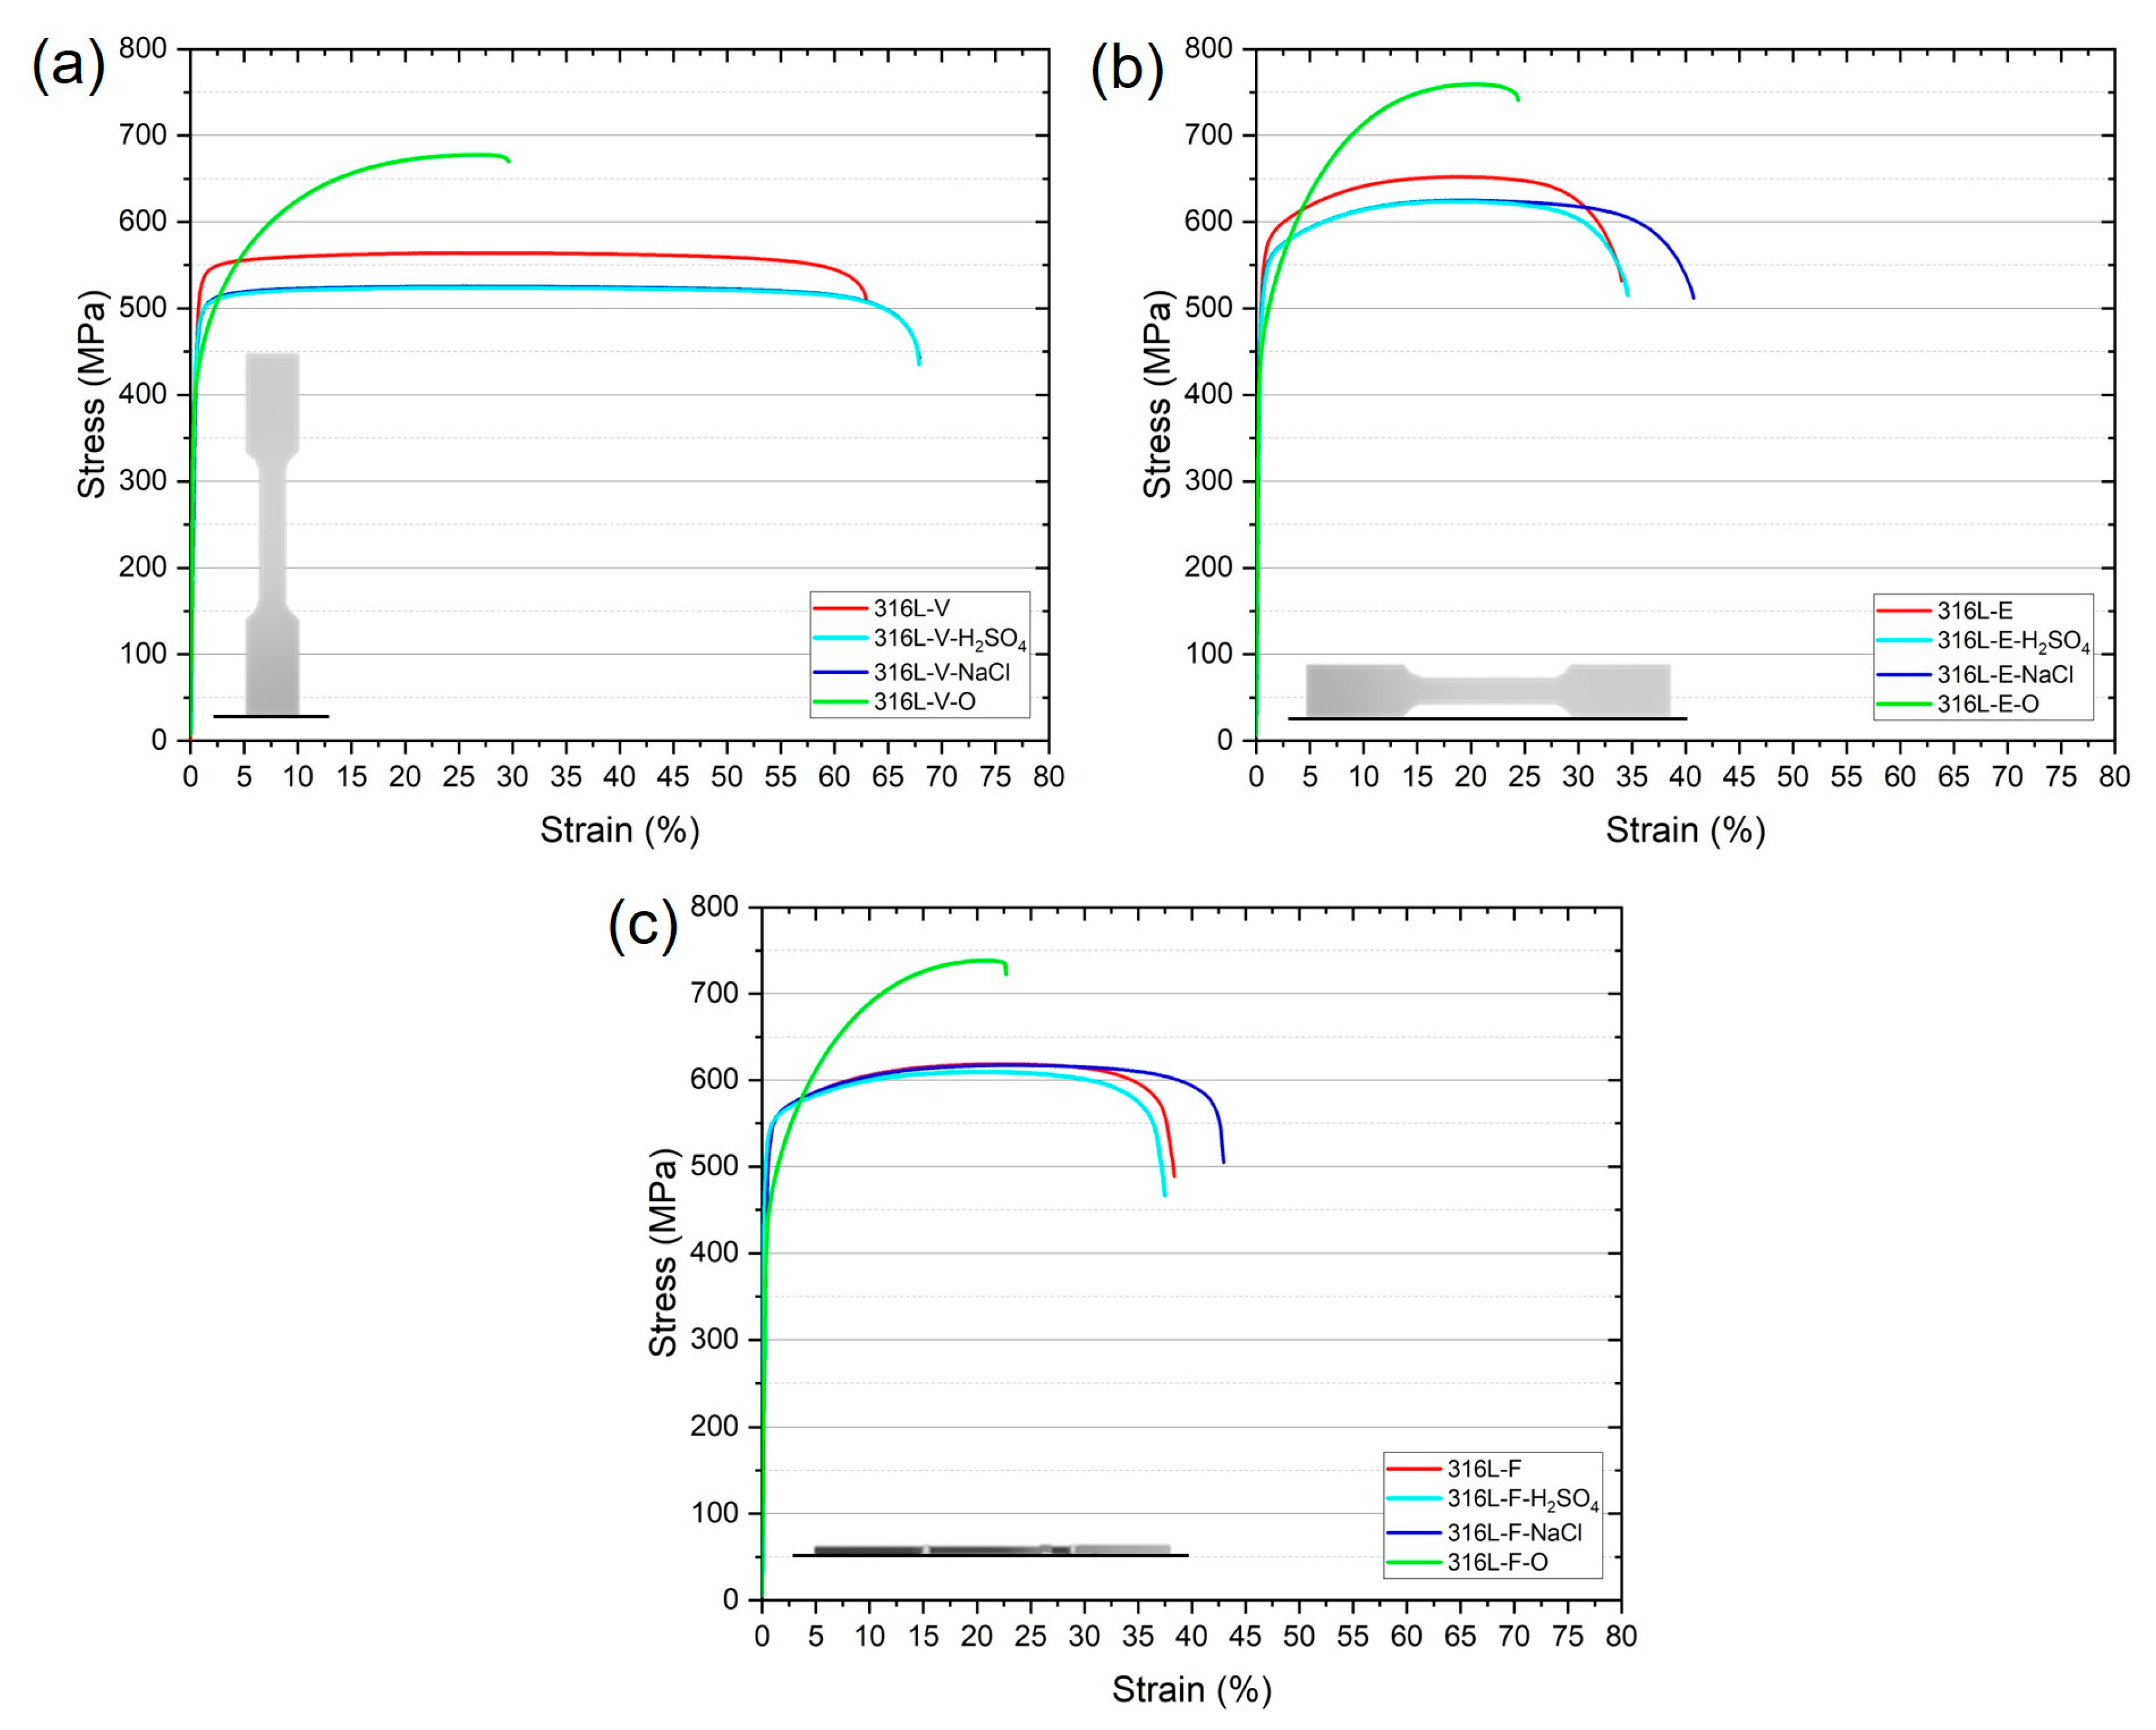
Figure 10 presents the representative engineering stress–strain curves of the L-PBF 316L stainless steel tested under different aggressive environments, considering each building orientation. A clear distinction can be observed between the curves corresponding to the oxidised condition (316L-O) and those of the as-built samples, as well as the specimens exposed to NaCl and H2SO4 environments. The results highlight that the mechanical performance of L-PBF 316L stainless steel is highly sensitive to long-term thermal exposure, which drastically alters both strength and ductility. In contrast, the influence of aggressive aqueous environments like NaCl and H2SO4 is more moderate and primarily surface-related.
Figure 10.
Representative engineering stress–strain curves of the L-PBF 316L ss according to the aggressive environment and building orientation: (a) vertical, (b) edge, and (c) flat.
In particular, the stress–strain plots of the 316L-O samples display a markedly different shape, characterised by a less defined yield point. This behaviour is attributed to the significant microstructural transformation that occurs after prolonged exposure to high temperatures. The alloy undergoes oxidation and microstructural coarsening, leading to a notable increase in tensile strength. However, this gain comes at the expense of ductility and yield strength, which decrease considerably due to the loss of strain-hardening capability and the embrittling effect of oxidation.
By contrast, the effect of immersion in NaCl and H2SO4 solutions on the engineering stress–strain curves are comparatively less severe because the microstructure of the stainless steel remains unchanged. Nevertheless, subtle modifications in mechanical response are detected in comparison with the as-built condition. These differences are linked to surface degradation phenomena such as delamination, localised corrosion, pit formation, or passive-film destabilisation (Figure 4 and Figure 5), which may affect the effective load-bearing area and slightly alter the plastic deformation behaviour.
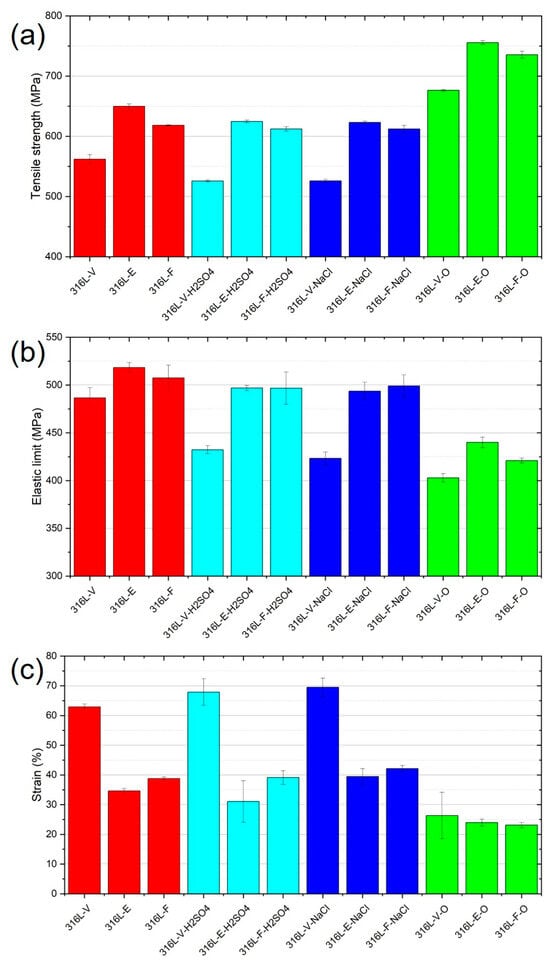
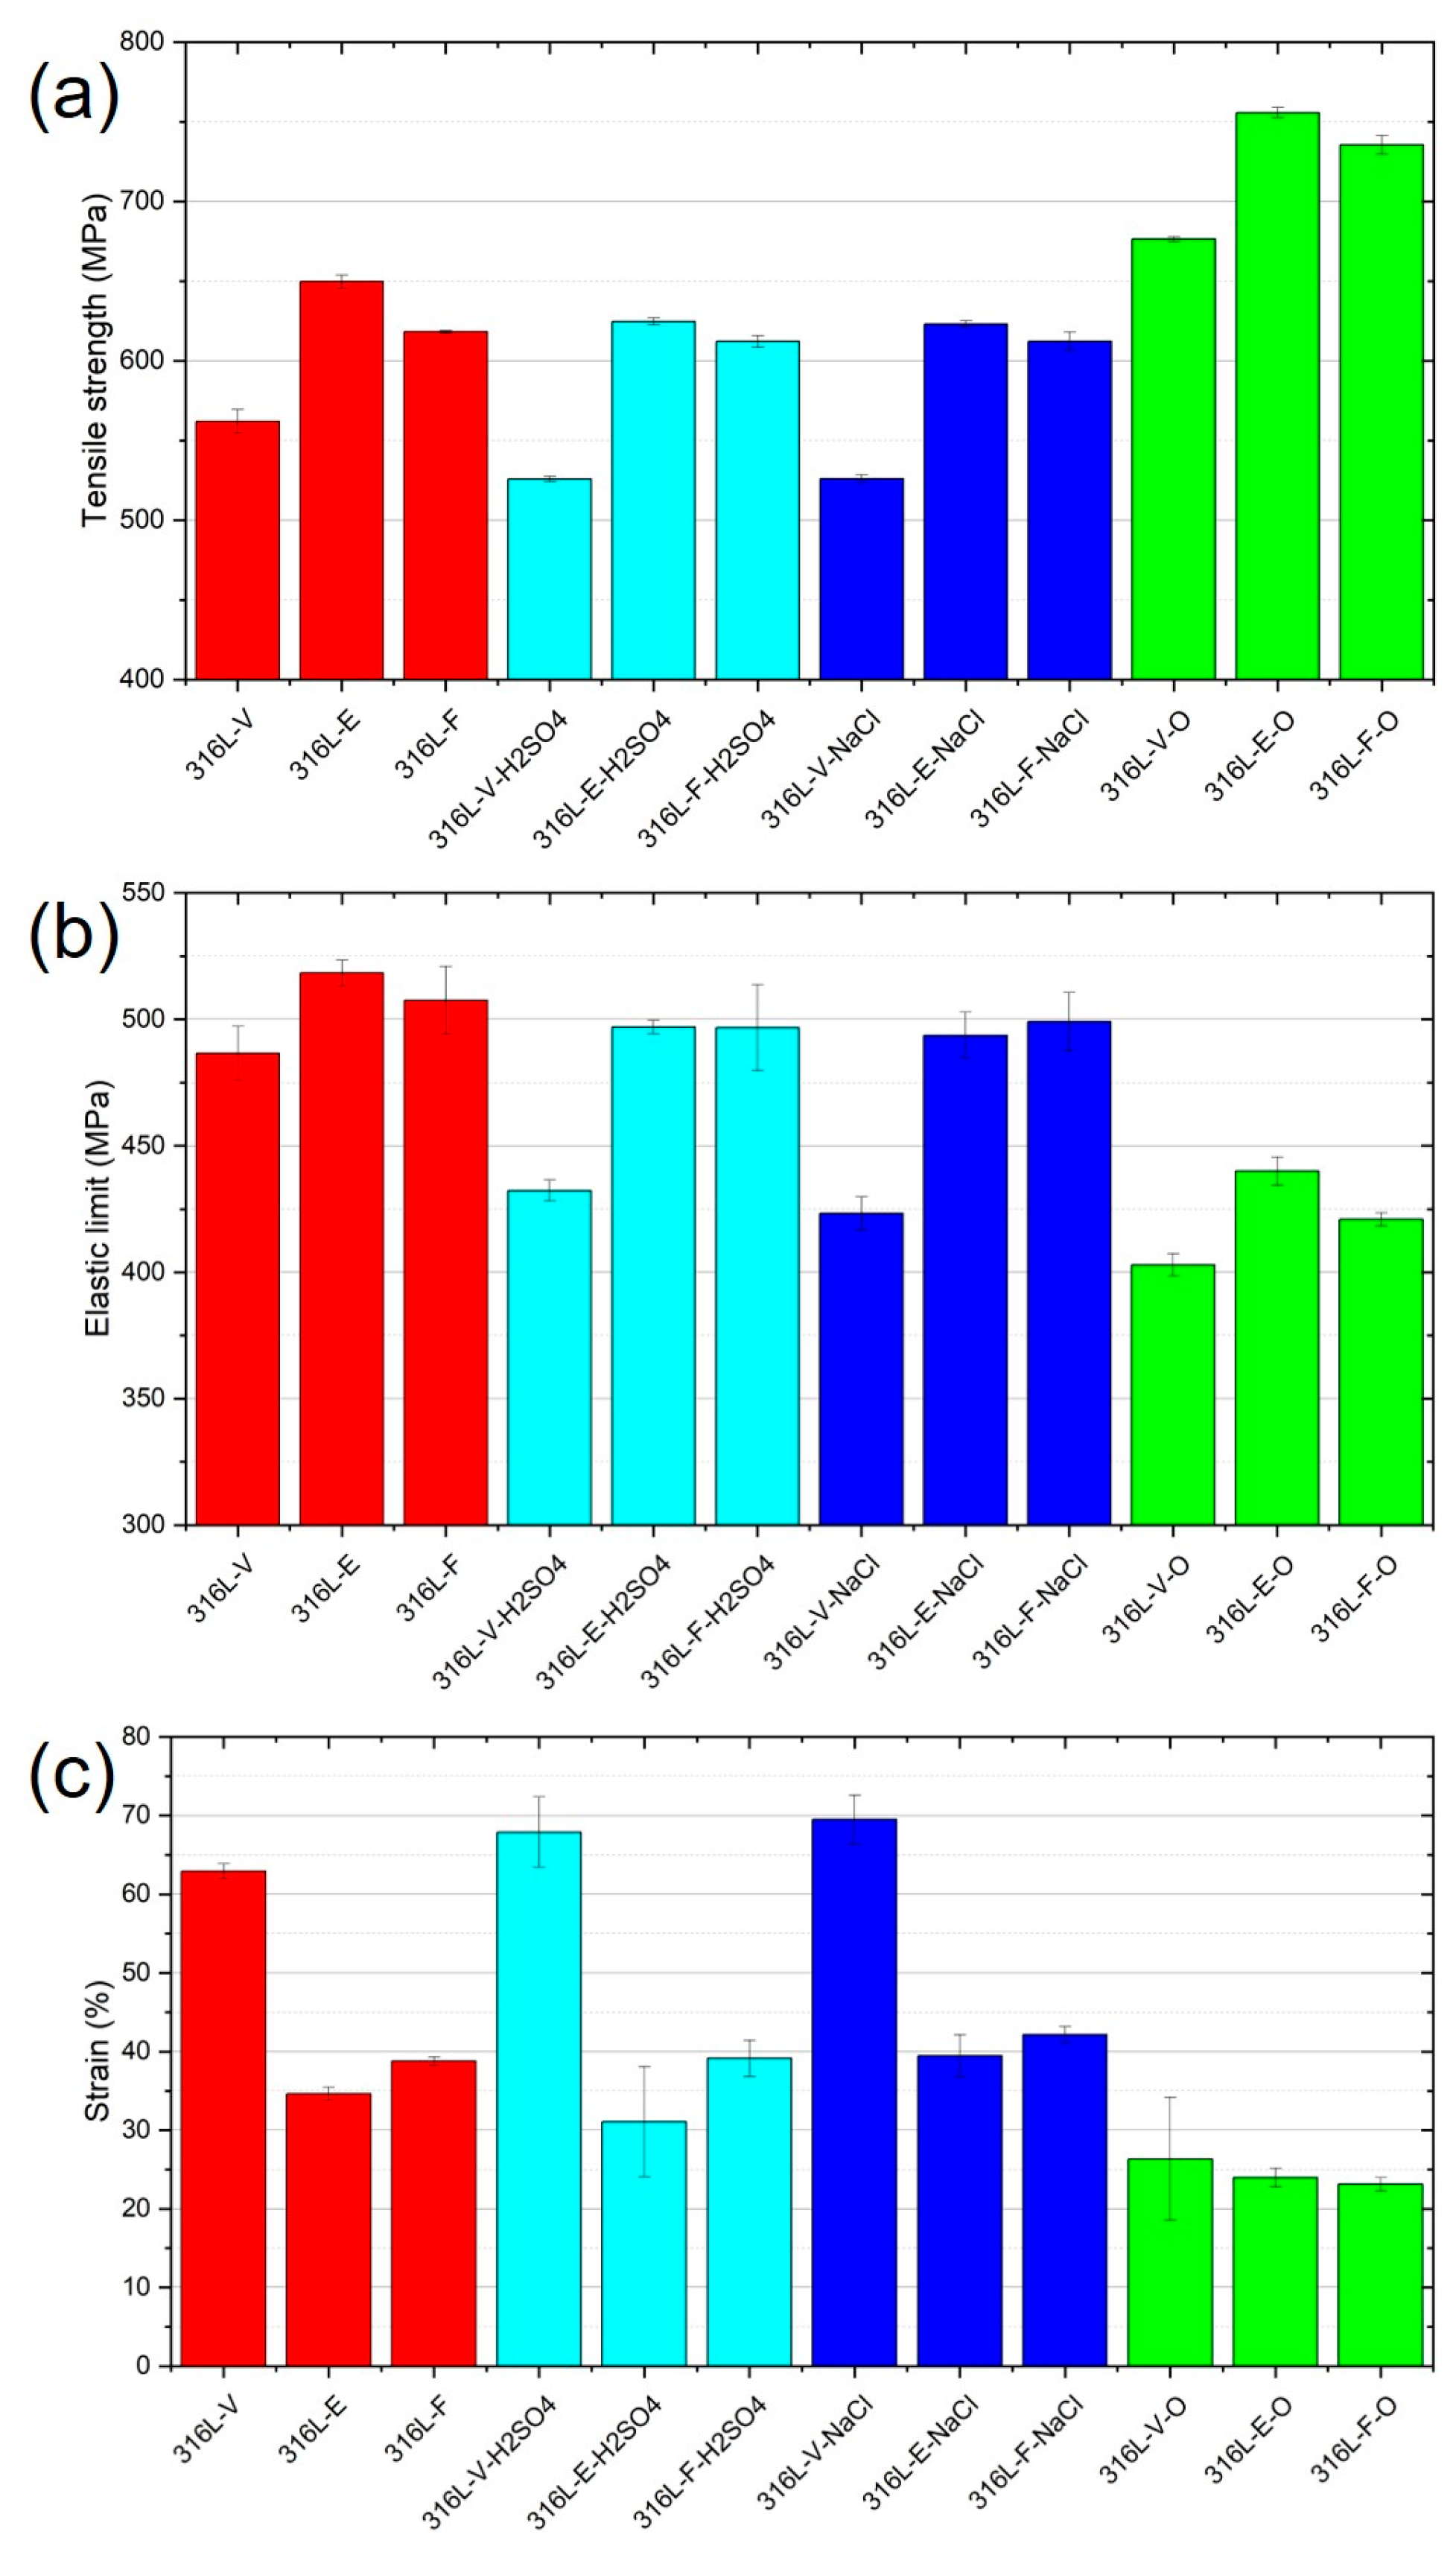
Figure 11 summarises the average values of tensile strength, yield strength, and strain obtained from the tested samples, providing a clearer framework for analysing the engineering stress–strain curves previously reported in Figure 10. As discussed earlier, the stress–strain behaviour of the as-built 316L stainless steel samples is very similar to that of the specimens immersed in NaCl and H2SO4 solutions for 360 h. Nevertheless, although no drastic modifications of the curves are observed, this exposure time is sufficient to induce a measurable deterioration in the mechanical properties of the material, independent of the building orientation.
Figure 11.
Average results of (a) tensile strength (in MPa), (b) yield strength (in MPa), and (c) strain (in %), of the L-PBF 316L ss according to the aggressive environment and the building orientation.
The detrimental effect is more pronounced in vertically built specimens, which consistently exhibit the greatest reduction in both tensile strength and yield strength compared with edge- and flat-built samples. For instance, the 316L-V-NaCl sample shows a ~6% reduction in tensile strength relative to the as-built 316L-V counterpart. In contrast, the 316L-E-NaCl and 316L-F-NaCl specimens display smaller decreases, around 4% and 1%, respectively. A similar tendency is found for the H2SO4-exposed samples, where the 316L-V-H2SO4 specimen also experiences the highest reduction in tensile strength (~6%) compared with its unexposed equivalent.
The yield strength follows the same orientation-dependent trend. For the vertically built samples, the reduction is significant, about 13% and 11% after immersion in NaCl and H2SO4, respectively. Meanwhile, edge- and flat-oriented samples undergo only minor reductions of approximately 4% and 2%, regardless of the solution. These findings highlight the critical influence of the building orientation on how aggressive media degrade the mechanical performance of L-PBF 316L stainless steel.
The layer-by-layer nature of the L-PBF process can explain this orientation-dependent degradation. In vertical builds, the stacking of layers generates microstructural features and surface conditions that increase susceptibility to environmental attack. The observations of this study are consistent with previous reports in the literature. Guzmán-Nogales et al. [41] demonstrated that surface orientation strongly influences the corrosion behaviour of L-PBF 316L stainless steel when exposed to 3.5 wt.% NaCl and 20% H2SO4 solutions. They emphasised that, in the absence of severe manufacturing defects such as lack of fusion or porosity, the crystallographic orientation and surface morphology are decisive factors governing passive film stability and corrosion resistance. Similarly, Yousif et al. [49] investigated corrosion resistance as a function of building orientation (0°, 45°, and 90°). They found that samples built at 0°, the flat orientation (316L-F) in the present study, exhibited superior resistance to pitting corrosion and lower susceptibility to pit initiation compared with 90° samples, the vertical orientation (316L-V) in the present study. This improved resistance was attributed to the denser microstructure, coarser grain size, reduced void fraction, and fewer surface defects typically associated with the flat orientation. In this context, vertical builds are particularly vulnerable, underscoring the importance of considering build orientation not only for mechanical performance in the as-built state but also for long-term durability in aggressive environments. It is also important to note that the as-built surface roughness acted as a stress concentrator, influencing fracture initiation in an orientation-dependent manner. Vertical builds exhibited a higher susceptibility due to the alignment of surface features with the loading direction, whereas edge and flat orientations mitigated this effect.
On the other hand, a significant increase in tensile strength was observed in the samples exposed to 800 °C for 360 h. Specifically, the 316L-V-O, 316L-E-O, and 316L-F-O specimens exhibited increases of approximately 20%, 16%, and 19%, respectively, when compared with their as-built counterparts. In this case, the high-temperature oxidation process acted analogously to a heat treatment, promoting precipitation hardening and microstructural reconfiguration. Unlike the behaviour reported in aggressive aqueous environments, the influence of building orientation on the mechanical performance was negligible under these thermal conditions. However, this improvement in tensile strength was accompanied by a drastic reduction in ductility.
This behaviour is directly related to the microstructural transformations revealed in Figure 7. The most critical change was the precipitation of the σ phase, which induced a strong hardening effect by hindering dislocation mobility, thus increasing tensile strength. Nevertheless, the same σ-phase precipitation also caused a reduction in toughness and elongation, since it embrittles the microstructure [50]. Similar findings have been reported by Jo et al. [51], who demonstrated that the σ phase can contribute positively to strength by acting as a dislocation barrier, while simultaneously compromising ductility. The σ-phase acts as a potent barrier to dislocation movement, enhancing strength via precipitation hardening. However, its brittle nature and tendency to precipitate at grain boundaries (σ1) promote crack initiation and reduce cohesive strength, leading to embrittlement and lowered ductility. This dual role explains the opposing trends in tensile strength versus yield strength and elongation. The mechanical response observed after oxidation are consistent with the documented effects of σ-phase precipitation in stainless steels. This correlation confirms that the phase identified by EDS is indeed σ-phase, despite the slight deviation in Ni content.
Furthermore, although new and larger austenite grains were observed to nucleate and grow in the 316L-O samples, they did not produce the expected theoretical effect, namely, a decrease in strength and an increase in ductility [52]. This suggests that the strengthening effect of the dispersed σ phase was more influential than the softening expected from grain coarsening. This interpretation is reinforced by the observation that the σ phase also precipitated at grain boundaries (σ1 in Figure 7b), exerting a grain boundary pinning effect that limited grain growth and effectively refined the microstructure in certain regions.
Nonetheless, the grain coarsening that occurred during the heat treatment cannot be disregarded. While σ-phase precipitation dominated the strengthening behaviour, the coarsening of the austenite matrix likely contributed to the reduction in yield strength observed across all orientations. Quantitatively, the yield strength decreased by approximately 17%, 15%, and 17% for the 316L-V-O, 316L-E-O, and 316L-F-O samples, respectively, compared to the as-built condition (see Figure 11b). This dual effect—precipitation hardening due to σ-phase formation and yield strength reduction due to grain coarsening—highlights the complex balance of competing mechanisms that govern the final mechanical performance of the oxidised samples.
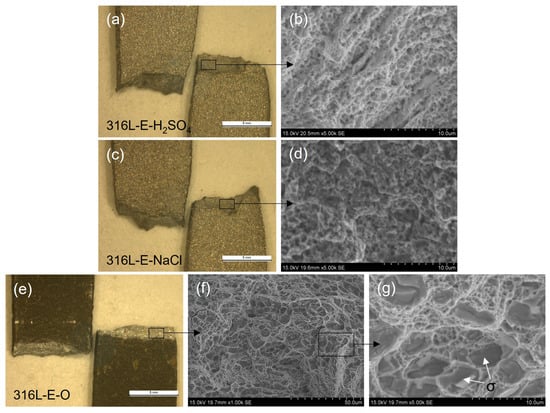
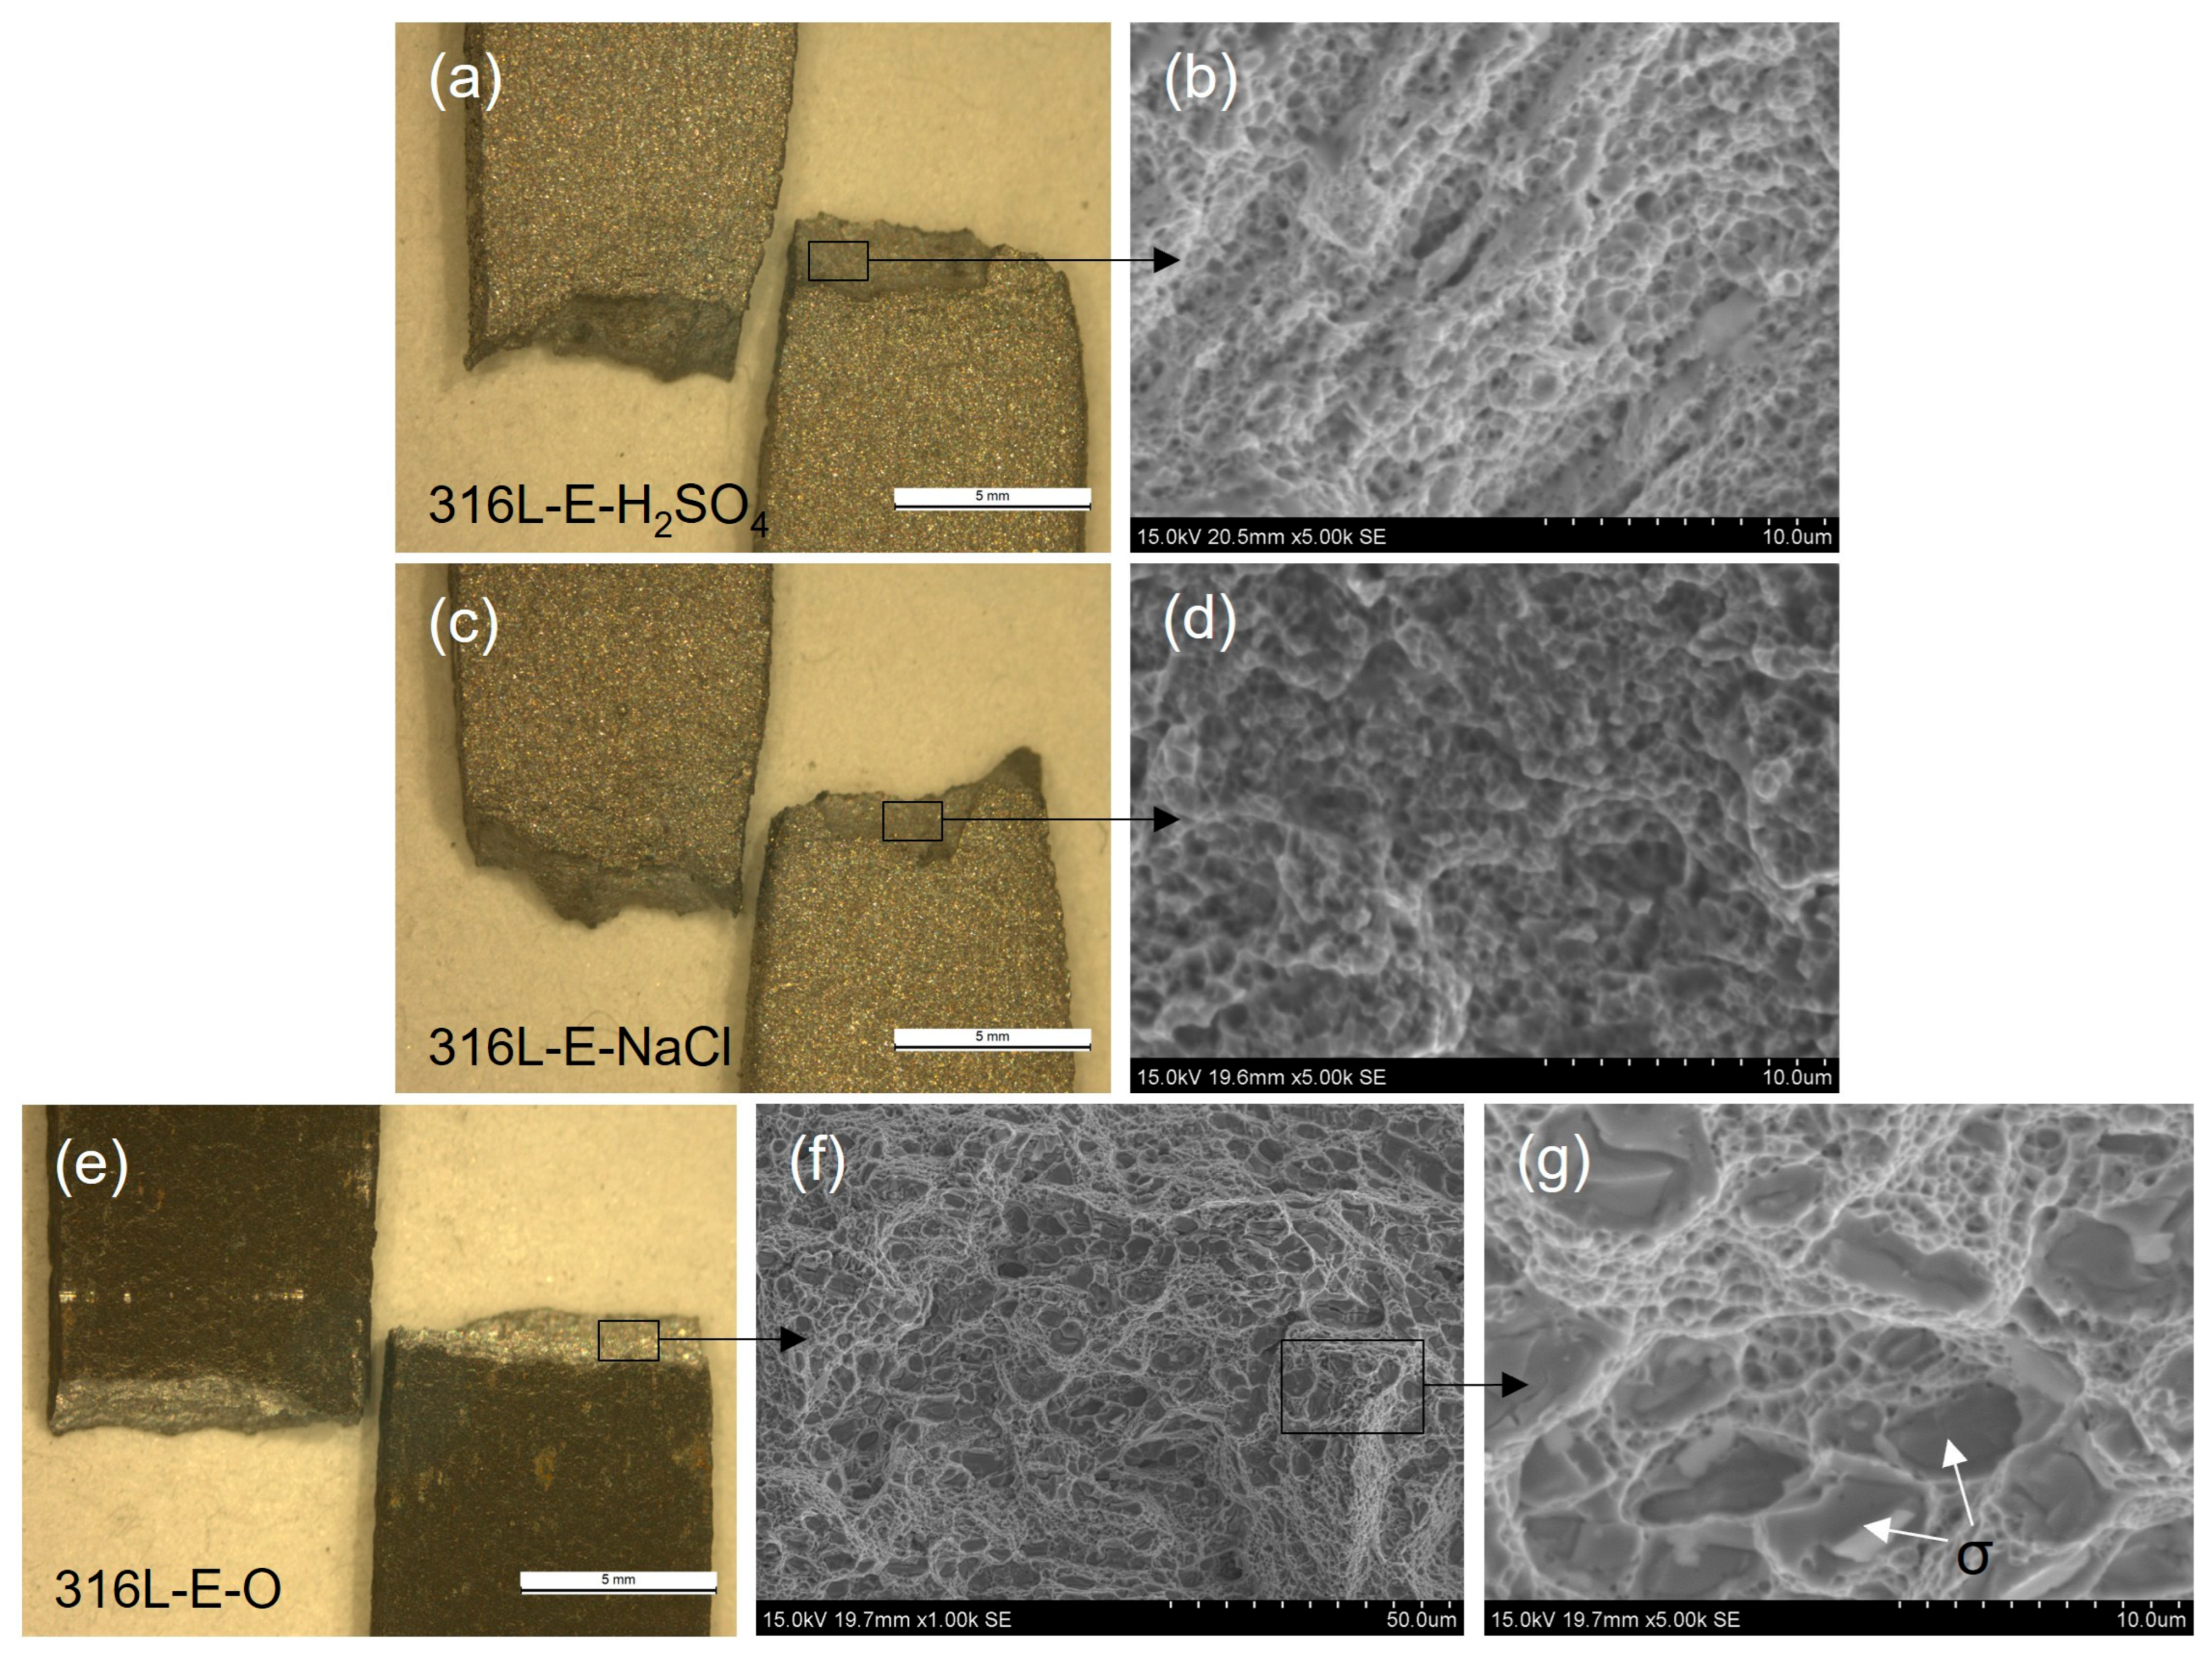
Figure 12 presents the fracture surfaces of the 316L-E samples after exposure to different aggressive environments. The fracture morphologies of the 316L-E-NaCl (Figure 12a,b) and 316L-E-H2SO4 (Figure 12c,d) specimens are comparable to those observed in the as-built 316L-E samples previously in Figure 9d–f, with no remarkable differences in surface features. This suggests that immersion in NaCl and H2SO4 solutions, despite causing slight degradation in mechanical properties, does not significantly alter the fracture mechanisms of the alloy.
Figure 12.
Optical and microstructural characterisation of the fractured surface of (a,b) 316L-E-H2SO4, (c,d) 316L-E-NaCl, and (e–g) 316L-E-O samples after tensile strength tests at different magnifications.
In contrast, the 316L-E-O sample reveals significant changes relative to its as-built counterpart. At low magnification (Figure 12e), the fracture surface appears noticeably flatter, with a less well-defined cup and cone morphology. This morphological change correlates with the reduced ductility observed in the mechanical tests, as the material loses its ability to undergo extensive plastic deformation prior to failure. At higher magnifications (Figure 12f,g), SEM micrographs reveal dimples that are considerably larger than those in the as-built specimens (Figure 9f). This increase in dimple size is attributed to the grain coarsening induced by recrystallization during exposure at 800 °C, as confirmed by the microstructural observations in Figure 7.
Interestingly, the enlarged grain size in the oxidised samples did not lead to a reduction in tensile strength. This contrasts with the findings of Wang et al. [53] and Zhong et al. [54], who reported that smaller grain sizes typically enhance tensile strength through grain boundary strengthening, since a higher number of grain boundaries act as barriers to dislocation movement. In the present case, the predominant strengthening mechanism is instead the precipitation of the σ phase, which exerts a more decisive influence on the mechanical response. According to precipitation strengthening theory, σ-phase particles hinder dislocation mobility, thereby increasing strength even in the presence of grain growth. The presence of σ-phase precipitates is corroborated by their direct observation on the fracture surface (arrows marked in Figure 12g).
Additionally, the oxidation process appears to improve fracture surface quality by eliminating defects inherent to the as-built condition. Unlike the fractured surfaces of the as-built specimens, the 316L-E-O sample does not display partially melted particles (Figure 12f). The disappearance of such unmelted particles, together with the reduction in microsegregations, lack of fusion zones, and porosity, indicates that the high-temperature oxidation treatment acted simultaneously as a post-processing heat treatment, homogenising the microstructure and enhancing load-bearing capacity. This effect, in combination with σ-phase precipitation, explains the significant increase in tensile strength reported for oxidised samples.
This work has provided a detailed understanding of how the combination of processing orientation and exposure to aggressive environments governs the mechanical response of L-PBF 316L stainless steel. The study has shown that aqueous media, such as NaCl and H2SO4 solutions, primarily induce surface-level degradation with orientation-dependent effects, while high-temperature oxidation generates bulk microstructural transformations that strongly modify strength and ductility. Beyond identifying the role of σ-phase precipitation, the research highlights how additive manufacturing enables not only high-performance components but also materials whose long-term reliability is deeply influenced by their microstructural anisotropy and service environment. Future research should explore strategies to mitigate σ-phase precipitation during high-temperature exposure, such as optimised alloying or tailored heat treatments, while maintaining the beneficial strengthening mechanisms provided by L-PBF. Likewise, a deeper correlation between microstructural orientation, passive film stability, and localised corrosion resistance in these environments is needed to improve predictive models of in-service behaviour. Extending this work to fatigue and creep resistance would further clarify the operational limits of L-PBF 316L, opening pathways to its safe implementation in critical applications such as energy, aerospace, and biomedical devices.
4. Conclusions
Edge- and flat-built samples (316L-E, 316L-F) exhibited higher tensile and yield strength than vertically built samples (316L-V), whereas the latter showed superior ductility. This anisotropic behaviour is associated with epitaxial grain growth, layer stacking, and the heterogeneous distribution of defects inherent to the L-PBF process. Additionally, the as-built surface roughness acted as a stress concentrator, influencing fracture initiation in an orientation-dependent manner. Vertical builds exhibited a higher susceptibility due to the alignment of surface features with the loading direction, whereas edge and flat orientations mitigated this effect.
Both NaCl and H2SO4 solutions induced only superficial degradation in the L-PBF 316L. However, reductions in tensile strength and yield strength were recorded, with 316L-V samples being the most affected. This highlights the role of building orientation in governing corrosion-assisted mechanical degradation.
The susceptibility of vertically built specimens to mechanical properties loss in aggressive aqueous environments is explained by the alignment of melt pool boundaries and defects in the loading direction. Edge and flat orientations provided enhanced resistance to mechanical degradation under identical conditions.
High-temperature oxidation at 800 °C produced a substantial increase in tensile strength (up to ~20%) due to σ-phase precipitation, which acted as a strengthening mechanism. At the same time, ductility and yield strength decreased significantly. In that case, building orientation had a negligible effect under oxidation conditions compared with its effect under aqueous environments.
Samples exposed to NaCl and H2SO4 retained ductile fracture characteristics like the as-built state. In contrast, oxidised samples exhibited flatter surfaces, enlarged dimples, and σ-phase precipitates, confirming the embrittling effect and its predominant influence on fracture mechanisms.
The long-term mechanical reliability of L-PBF 316L stainless steel depends strongly on service conditions. Aqueous environments primarily affect surface integrity in an orientation-sensitive manner, whereas high-temperature oxidation induces bulk microstructural transformations with opposing effects on strength and ductility. These results underline the importance of carefully selecting build orientation strategy to optimise performance for specific industrial environments.
For industrial applications, selecting edge or flat build orientations is recommended for components exposed to corrosive environments, as these configurations offer superior resistance to mechanical degradation. Additionally, for parts intended for high-temperature service, post-processing techniques should be considered to mitigate embrittlement associated with σ-phase precipitation while maintaining the benefits of precipitation hardening.
Author Contributions
N.A.-w.: conceptualization, methodology, formal analysis, investigation, writing—original draft. J.B.: conceptualization, methodology, formal analysis, investigation, writing—original draft. S.G.-R.: conceptualization, methodology, formal analysis, investigation, writing—review and editing. B.T.: supervision, writing—review and editing, funding acquisition, project administration. J.R.: supervision, writing—review and editing, funding acquisition, project administration. All authors have read and agreed to the published version of the manuscript.
Funding
This research was funded by Ministerio de Ciencia e Innovación of Spain (Project PLEC2023-010346) and Universidad Rey Juan Carlos (Project 2024/SOLCON-137629).
Data Availability Statement
The data presented in this study are available on request from the corresponding author. The data are not publicly available due to privacy restrictions.
Conflicts of Interest
The authors declare no conflicts of interest.
References
- Murugan, P.D.; Vijayananth, S.; Natarajan, M.P.; Jayabalakrishnan, D.; Arul, K.; Jayaseelan, V.; Elanchezhian, J. A current state of metal additive manufacturing methods: A review. Mater. Today Proc. 2022, 59, 1277–1283. [Google Scholar] [CrossRef] [Scilit]
- Yang, J.; Gu, D.; Lin, K.; Zhang, Y.; Guo, M.; Yuan, L.; Zhang, H.; Zhang, H. Laser Additive Manufacturing of Bio-inspired Metallic Structures. Chinese J. Mech. Eng. Addit. Manuf. Front. 2022, 1, 100013. [Google Scholar] [CrossRef] [Scilit]
- Abrami, M.B.; Tocci, M.; Obeidi, M.A.; Brabazon, D.; Pola, A. Prediction of Microstructure for AISI316L Steel from Numerical Simulation of Laser Powder Bed Fusion. Met. Mater. Int. 2022, 28, 2735–2746. [Google Scholar] [CrossRef] [Scilit]
- Monfared, V.; Ramakrishna, S.; Nasajpour-Esfahani, N.; Toghraie, D.; Hekmatifar, M.; Rahmati, S. Science and Technology of Additive Manufacturing Progress: Processes, Materials, and Applications. Met. Mater. Int. 2023, 29, 3442–3470. [Google Scholar] [CrossRef] [Scilit]
- Liang, A.; Pey, K.S.; Polcar, T.; Hamilton, A.R. Effects of rescanning parameters on densification and microstructural refinement of 316L stainless steel fabricated by laser powder bed fusion. J. Mater. Process. Technol. 2022, 302, 117493. [Google Scholar] [CrossRef] [Scilit]
- Afkhami, S.; Dabiri, M.; Piili, H.; Björk, T. Effects of manufacturing parameters and mechanical post-processing on stainless steel 316L processed by laser powder bed fusion. Mater. Sci. Eng. A 2021, 802, 140660. [Google Scholar] [CrossRef] [Scilit]
- Petroušek, P.; Kočiško, R.; Kasperkevičová, A.; Csík, D.; Džunda, R. Effect of Thermomechanical Processing on Porosity Evolution and Mechanical Properties of L-PBF AISI 316L Stainless Steel. Metals 2025, 15, 789. [Google Scholar] [CrossRef] [Scilit]
- Gilat, A.; Kuokkala, V.T.; Seidt, J.D.; Smith, J.L. Full-Field Measurement of Strain and Temperature in Quasi-Static and Dynamic Tensile Tests on Stainless Steel 316L. Procedia Eng. 2017, 207, 1994–1999. [Google Scholar] [CrossRef] [Scilit]
- Li, M.; Chen, W.Y.; Zhang, X. Effect of heat treatment on creep behavior of 316 L stainless steel manufactured by laser powder bed fusion. J. Nucl. Mater. 2022, 559, 153469. [Google Scholar] [CrossRef] [Scilit]
- Revilla, R.I.; Wouters, B.; Andreatta, F.; Lanzutti, A.; Fedrizzi, L.; De Graeve, I. EIS comparative study and critical Equivalent Electrical Circuit (EEC) analysis of the native oxide layer of additive manufactured and wrought 316L stainless steel. Corros. Sci. 2020, 167, 108480. [Google Scholar] [CrossRef] [Scilit]
- S, D.; Sahu, J. A Comprehensive Review on Laser Powder Bed Fusion Process of SS316L Mechanical Properties and Post-Processing. Met. Mater. Int. 2026, 32, 106–138. [Google Scholar] [CrossRef] [Scilit]
- He, X.; Shang, X.K.; He, J.; He, B.B. Influence of dislocation cell on the thermomechanical stability of 316 L fabricated by laser powder bed fusion. Mater. Charact. 2024, 217, 114335. [Google Scholar] [CrossRef] [Scilit]
- Liu, W.; Liu, C.; Wang, Y.; Zhang, H.; Li, J.; Lu, Y.; Xiong, L.; Ni, H. Tailoring the microstructural and mechanical properties of 316L stainless steel manufactured by laser powder bed fusion. J. Mater. Res. Technol. 2023, 25, 7389–7405. [Google Scholar] [CrossRef] [Scilit]
- Bedmar, J.; Riquelme, A.; Rodrigo, P.; Torres, B.; Rams, J. Comparison of different additive manufacturing methods for 316L stainless steel. Materials 2021, 14, 6504. [Google Scholar] [CrossRef] [Scilit]
- Cruz, V.; Qiu, Y.; Birbilis, N.; Thomas, S. Stress corrosion cracking of 316L manufactured by laser powder bed fusion in 6% ferric chloride solution. Corros. Sci. 2022, 207, 110535. [Google Scholar] [CrossRef] [Scilit]
- Efremenko, B.; Chabak, Y.; Petryshynets, I.; Zhao, T.; Efremenko, V.; Wu, K.; Xia, T.; Džupon, M.; Arshad, S. Evaluation of the Suitability of High-Temperature Post-Processing Annealing for Property Enhancement in LPBF 316L Steel: A Comprehensive Mechanical and Corrosion Assessment. Metals 2025, 15, 684. [Google Scholar] [CrossRef] [Scilit]
- Suryawanshi, J.; Prashanth, K.G.; Ramamurty, U. Mechanical behavior of selective laser melted 316L stainless steel. Mater. Sci. Eng. A 2017, 696, 113–121. [Google Scholar] [CrossRef] [Scilit]
- Jagannati, V.; Gurram, M.; Turaka, S.; Naidu, B.V.V.; Verma, G.K.; Krishnan, P.K.; Sarimalla, R.; Sebaey, T.A.; Bandaru, A.K. Review of tensile anisotropy in laser powder bed fusion 316L stainless steel: Build orientation effects and optimisation using machine learning. J. Mater. Res. Technol. 2025, 38, 5318–5341. [Google Scholar] [CrossRef] [Scilit]
- Charmi, A.; Falkenberg, R.; Ávila, L.; Mohr, G.; Sommer, K.; Ulbricht, A.; Sprengel, M.; Neumann, R.S.; Skrotzki, B.; Evans, A. Mechanical anisotropy of additively manufactured stainless steel 316L: An experimental and numerical study. Mater. Sci. Eng. A 2021, 799, 140154. [Google Scholar] [CrossRef] [Scilit]
- Kurian, S.; Mirzaeifar, R. Deformation mechanisms of the subgranular cellular structures in selective laser melted 316L stainless steel. Mech. Mater. 2020, 148, 103478. [Google Scholar] [CrossRef] [Scilit]
- Wang, C.; Lin, X.; Wang, L.; Zhang, S.; Huang, W. Cryogenic mechanical properties of 316L stainless steel fabricated by selective laser melting. Mater. Sci. Eng. A 2021, 815, 141317. [Google Scholar] [CrossRef] [Scilit]
- Sangoi, K.; Nadimi, M.; Song, J.; Fu, Y. Heat Treatment Effect on the Corrosion Resistance of 316L Stainless Steel Produced by Laser Powder Bed Fusion. Metals 2025, 15, 41. [Google Scholar] [CrossRef] [Scilit]
- Vukkum, V.B.; Gupta, R.K. Review on corrosion performance of laser powder-bed fusion printed 316L stainless steel: Effect of processing parameters, manufacturing defects, post-processing, feedstock, and microstructure. Mater. Des. 2022, 221, 110874. [Google Scholar] [CrossRef] [Scilit]
- Kong, D.; Dong, C.; Ni, X.; Zhang, L.; Yao, J.; Man, C.; Cheng, X.; Xiao, K.; Li, X. Mechanical properties and corrosion behavior of selective laser melted 316L stainless steel after different heat treatment processes. J. Mater. Sci. Technol. 2019, 35, 1499–1507. [Google Scholar] [CrossRef] [Scilit]
- Sander, G.; Thomas, S.; Cruz, V.; Jurg, M.; Birbilis, N.; Gao, X.; Brameld, M.; Hutchinson, C.R. On The Corrosion and Metastable Pitting Characteristics of 316L Stainless Steel Produced by Selective Laser Melting. J. Electrochem. Soc. 2017, 164, C250–C257. [Google Scholar] [CrossRef] [Scilit]
- Nie, J.; Wei, L.; Jiang, Y.; Li, Q.; Luo, H. Corrosion mechanism of additively manufactured 316 L stainless steel in 3.5 wt.% NaCl solution. Mater. Today Commun. 2021, 26, 101648. [Google Scholar] [CrossRef] [Scilit]
- Loto, R.T. Study of the corrosion resistance of type 304L and 316 austenitic stainless steels in acid chloride solution. Orient. J. Chem. 2017, 33, 1090–1096. [Google Scholar] [CrossRef] [Scilit]
- Lodhi, M.J.K.; Deen, K.M.; Haider, W. Corrosion behavior of additively manufactured 316L stainless steel in acidic media. Materialia 2018, 2, 111–121. [Google Scholar] [CrossRef] [Scilit]
- Yeganeh, M.; Rezvani, M.H.; Laribaghal, S.M. Electrochemical behavior of additively manufactured 316L stainless steel in H2SO4 solution containing methionine as an amino acid. Colloids Surf. A Physicochem. Eng. Asp. 2021, 627, 127120. [Google Scholar] [CrossRef] [Scilit]
- Bedmar, J.; Abu-warda, N.; García-Rodríguez, S.; Torres, B.; Rams, J. Influence of the surface state on the corrosion behavior of the 316 L stainless steel manufactured by laser powder bed fusion. Corros. Sci. 2022, 207, 110550. [Google Scholar] [CrossRef] [Scilit]
- Abu-warda, N.; García-Rodríguez, S.; Torres, B.; Utrilla, M.V.; Rams, J. Impact of the additive manufacturing process on the high-temperature corrosion of 316L steel in the presence of NaCl–KCl–ZnCl2 molten solar salt. J. Mater. Res. Technol. 2022, 20, 3949–3961. [Google Scholar] [CrossRef] [Scilit]
- Abu-warda, N.; García-Rodríguez, S.; Torres, B.; Utrilla, M.V.; Rams, J. Effect of Molten Salts Composition on the Corrosion Behavior of Additively Manufactured 316L Stainless Steel for Concentrating Solar Power. Metals 2024, 14, 639. [Google Scholar] [CrossRef] [Scilit]
- Siri, C.; Popa, I.; Vion, A.; Langlade, C.; Chevalier, S. Impact of Selective Laser Melting Additive Manufacturing on the High Temperature Behavior of AISI 316L Austenitic Stainless Steel. Oxid. Met. 2020, 94, 527–548. [Google Scholar] [CrossRef] [Scilit]
- Trisnanto, S.R.; Wang, X.; Brochu, M.; Omanovic, S. Effects of crystallographic orientation on the corrosion behavior of stainless steel 316L manufactured by laser powder bed fusion. Corros. Sci. 2022, 196, 110009. [Google Scholar] [CrossRef] [Scilit]
- Sander, G.; Babu, A.P.; Gao, X.; Jiang, D.; Birbilis, N. On the effect of build orientation and residual stress on the corrosion of 316L stainless steel prepared by selective laser melting. Corros. Sci. 2021, 179, 109149. [Google Scholar] [CrossRef] [Scilit]
- Zhao, C.; Bai, Y.; Zhang, Y.; Wang, X.; Xue, J.M.; Wang, H. Influence of scanning strategy and building direction on microstructure and corrosion behaviour of selective laser melted 316L stainless steel. Mater. Des. 2021, 209, 109999. [Google Scholar] [CrossRef] [Scilit]
- Fedorenko, A.; Fedulov, B.; Kuzminova, Y.; Evlashin, S.; Staroverov, O.; Tretyakov, M.; Lomakin, E.; Akhatov, I. Anisotropy of Mechanical Properties and Residual Stress in Additively Manufactured 316L Specimens. Materials 2021, 14, 7176. [Google Scholar] [CrossRef] [Scilit]
- Dixit, S.; Liu, S.; Murdoch, H.A.; Smith, P.M. Investigating build orientation-induced mechanical anisotropy in additive manufacturing 316L stainless steel. Mater. Sci. Eng. A 2023, 880, 145308. [Google Scholar] [CrossRef] [Scilit]
- ISO 6892-1:2019; Metallic Materials—Tensile Testing—Part 1: Method of Test at Room Temperature. International Organization for Standardization: Geneva, Switzerland, 2019.
- Herzog, D.; Seyda, V.; Wycisk, E.; Emmelmann, C. Additive manufacturing of metals. Acta Mater. 2016, 117, 371–392. [Google Scholar] [CrossRef] [Scilit]
- Guzmán-Nogales, R.; Estupiñán-López, F.; Gaona-Tiburcio, C.; Lopez-Botello, O.E.; Ramírez-Rodríguez, J.G.; Zambrano-Robledo, P.C. Corrosion Resistance Measurement of 316L Stainless Steel Manufactured by Selective Laser Melting. Materials 2021, 14, 4509. [Google Scholar] [CrossRef] [Scilit]
- Abdelfatah, A.; Raslan, A.M.; Mohamed, L.Z. Corrosion Characteristics of 304 Stainless Steel in Sodium Chloride and Sulfuric Acid Solutions. Int. J. Electrochem. Sci. 2022, 17, 220417. [Google Scholar] [CrossRef] [Scilit]
- Yin, H.; Song, M.; Deng, P.; Li, L.; Prorok, B.C.; Lou, X. Thermal stability and microstructural evolution of additively manufactured 316L stainless steel by laser powder bed fusion at 500–800 °C. Addit. Manuf. 2021, 41, 101981. [Google Scholar] [CrossRef] [Scilit]
- Perron, A.; Toffolon-Masclet, C.; Ledoux, X.; Buy, F.; Guilbert, T.; Urvoy, S.; Bosonnet, S.; Marini, B.; Cortial, F.; Texier, G.; et al. Understanding sigma-phase precipitation in a stabilized austenitic stainless steel (316Nb) through complementary CALPHAD-based and experimental investigations. Acta Mater. 2014, 79, 16–29. [Google Scholar] [CrossRef] [Scilit]
- Villanueva, D.M.E.; Junior, F.C.P.; Plaut, R.L.; Padilha, A.F. Comparative study on sigma phase precipitation of three types of stainless steels: Austenitic, superferritic and duplex. Mater. Sci. Technol. 2006, 22, 1098–1104. [Google Scholar] [CrossRef] [Scilit]
- Casati, R.; Lemke, J.; Vedani, M. Microstructure and Fracture Behavior of 316L Austenitic Stainless Steel Produced by Selective Laser Melting. J. Mater. Sci. Technol. 2016, 32, 738–744. [Google Scholar] [CrossRef] [Scilit]
- Abu-warda, N.; Bedmar, J.; García-Rodriguez, S.; Torres, B.; Utrilla, M.V.; Rams, J. Effect of post-processing heat treatments on the high-temperature oxidation of additively manufactured 316L stainless steel. J. Mater. Res. Technol. 2024, 29, 3465–3476. [Google Scholar] [CrossRef] [Scilit]
- Tolosa, I.; Garciandía, F.; Zubiri, F.; Zapirain, F.; Esnaola, A. Study of mechanical properties of AISI 316 stainless steel processed by “selective laser melting”, following different manufacturing strategies. Int. J. Adv. Manuf. Technol. 2010, 51, 639–647. [Google Scholar] [CrossRef] [Scilit]
- Yousif, M.A.S.; Al-Deheish, I.A.; Ali, U.; Akhtar, S.S.; Al-Athel, K.S. Mechanical, tribological, and corrosion behavior of laser powder-bed fusion 316L stainless steel parts: Effect of build orientation. J. Mater. Res. Technol. 2024, 33, 1220–1233. [Google Scholar] [CrossRef] [Scilit]
- Hsieh, C.-C.; Wu, W. Overview of Intermetallic Sigma (σ) Phase Precipitation in Stainless Steels. ISRN Metall. 2012, 2012, 732471. [Google Scholar] [CrossRef] [Scilit]
- Jo, Y.H.; Choi, W.M.; Sohn, S.S.; Kim, H.S.; Lee, B.J.; Lee, S. Role of brittle sigma phase in cryogenic-temperature-strength improvement of non-equi-atomic Fe-rich VCrMnFeCoNi high entropy alloys. Mater. Sci. Eng. A 2018, 724, 403–410. [Google Scholar] [CrossRef] [Scilit]
- Wang, Y.; Xiao, B.; Liang, X.; Peng, H.; Zhou, J. Strengthened microstructure and mechanical properties of austenitic 316L stainless steels by grain refinement and solute segregation. J. Mater. Res. Technol. 2025, 34, 552–565. [Google Scholar] [CrossRef] [Scilit]
- Wang, D.; Song, C.; Yang, Y.; Bai, Y. Investigation of crystal growth mechanism during selective laser melting and mechanical property characterization of 316L stainless steel parts. Mater. Des. 2016, 100, 291–299. [Google Scholar] [CrossRef] [Scilit]
- Zhong, Y.; Liu, L.F.; Wikman, S.; Cui, D.Q.; Shen, Z.J. Intragranular cellular segregation network structure strengthening 316L stainless steel prepared by selective laser melting. J. Nucl. Mater. 2016, 470, 170–178. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.