


Abstract
Conventional particleboards often exhibit limited mechanical strength, which restricts their use in load-bearing and high-performance applications; reinforcing these boards with carbon fibers offers a potential solution to overcome these limitations. This study investigated the effect of carbon fiber (CF) content on the mechanical performance of single-layer particleboards bonded with polymeric methylene diphenyl diisocyanate (pMDI) adhesive. Carbon fibers were examined as a reinforcement to improve the mechanical properties of particleboards. Experimental boards were produced with 0, 10, 20, 30, 40, and 50% CF (based on the oven-dry mass of wood particles). The analysis included density profile distribution, modulus of rupture (MOR), modulus of elasticity (MOE), and screw withdrawal resistance (SWR). The results showed that mechanical performance improved only at lower CF contents. The most pronounced effect was observed at 10% CF, where MOR increased from 15.2 MPa (control) to 19.2 MPa, and MOE increased from 2.45 GPa to 2.91 GPa. Higher CF additions (≥20%) did not yield further improvements, and at elevated levels (≥30%), bending performance decreased (MOR dropped to 14.1–13.5 MPa) due to poor fiber dispersion and weakened interfacial bonding between fibers and wood particles. Screw withdrawal resistance increased gradually with CF content, from 156 N in the control boards to 182 N at 50% CF, although the improvement was limited by adhesion quality and mat heterogeneity. Overall, the study demonstrates that small CF additions can enhance selected mechanical properties of particleboards, whereas higher loadings negatively affect performance due to microstructural incompatibilities.
1. Introduction
Particleboards are widely used in the furniture and construction industries due to their cost-effectiveness and the sustainable utilization of wood residues. According to FAO data, global particleboard production reached 116.6 million m3 in 2023, with Europe accounting for 44.0 million m3, representing 37.7% of the global share [1]. Compared with 2020, this corresponds to an increase of more than 20% worldwide and 6.3% in Europe. The growing demand for wood-based panels, combined with raw material shortages and increasing environmental awareness, underscores the need to explore alternative feedstocks and optimize material properties.
Despite their widespread use, conventional particleboards are characterized by relatively low mechanical strength and high susceptibility to moisture, which limits their broader application. Moreover, competition for wood resources affects both availability and production costs. To enhance mechanical and hygroscopic performance, multiple strategies have been investigated, including the use of alternative raw materials, eco-friendly adhesives, and reinforcing agents. For instance, biopolymers such as polylactic acid (PLA), poly(ε-caprolactone) (PCL), and starch have been used as sustainable adhesives, resulting in improvements in mechanical and physical properties [2,3]. Similarly, incorporating fillers such as suberin-rich bark residues can positively influence panel performance when applied within specific limits [4,5]. Agricultural residues also constitute promising alternative feedstocks to industrial wood particles, including wheat straw, rice straw, bamboo, and palm particles, among others [6,7,8,9,10,11,12,13,14,15,16,17,18,19,20,21,22,23,24,25,26,27,28,29].
Parallel research has focused on particleboards reinforced with synthetic materials. For example, adding glass fabric to a three-layer panel (16 mm thickness, 700 kg/m3 density) enhanced bending strength by 8%–40% [30]. Čabalová et al. [31] used rubber waste from insulators and tires as a substitute for wood particles and found that 10% granulate did not diminish mechanical performance while improving thermal insulation. Hermawan et al. [32] applied 40% porcelain waste, which reduced thickness swelling and improved fire resistance, although with a slight decrease in MOR and MOE. Comparable numerical trends have been reported in studies incorporating alternative fibrous reinforcements. Zhang et al. [33] observed approximately a 40% increase in MOR when adding 30% recycled glass fibers to particleboards of similar density (~700 kg/m3). In contrast, the maximum MOR improvement obtained in the present study was 26% at a substantially lower reinforcement content (10% CF). Ishwanto et al. [34] reported MOR increments of 15%–30% in boards reinforced with glass fibers and organic waste particles, which is comparable to the improvement observed for the 10/90 variant. These findings indicate that moderate carbon fiber additions produce mechanical gains of similar magnitude to those reported for other synthetic and recycled fibers, although the efficiency of reinforcement depends strongly on fiber dispersion and interfacial adhesion.
In recent years, growing attention has shifted towards carbon fibers as reinforcement for wood-based panels. Their high stiffness and moisture resistance make them an attractive alternative to traditional glass fibers. Studies have shown that incorporating carbon fiber sheets into LVL can increase bending strength by approximately 30% compared to unmodified LVL [35]. Hybridization with basalt fibers has also been found to improve shear and compressive strength [36]. In glued laminated beams, carbon fiber strips enhance load-bearing capacity and load–displacement behavior, with effectiveness strongly dependent on fiber placement, particularly near the outer LVL layers. Research on plywood reinforced with carbon fabrics has demonstrated substantial improvements in mechanical strength and modulus of elasticity, as well as the potential for functional properties such as thermal and electrothermal conductivity [37]. Furthermore, CFs can be combined with formaldehyde-free adhesives, such as polyethylene grafted with maleic anhydride (MAPE), supporting environmentally friendly, high performance composites.
Nanomodification with carbon nanomaterials (CNMs), including nanotubes, nanofibers, and graphene, has also emerged as a promising approach to enhance strength, stiffness, water resistance, and functional attributes such as electrical conductivity, antistatic behavior, and heat dissipation [38,39,40]. Unlike conventional mineral fillers or coatings, carbon nanostructures can penetrate the porous wood structure, forming highly integrated composite systems. Their application aligns with efforts to develop eco-friendly composites with reduced synthetic resin content and expanded functional performance. Furthermore, emerging research focuses on converting wood and biomass residues into natural carbon nanostructures, supporting circular economy principles by reducing reliance on non-renewable resources and promoting sustainable material technologies.
Despite extensive research on fiber-reinforced wood composites, systematic studies on the effect of carbon fiber (CF) content on the mechanical and physical properties of single-layer particleboards remain scarce. Existing research provides limited data on optimal fiber content, distribution, and integration methods. Key challenges include ensuring fiber quality and uniformity, avoiding bonding issues or density heterogeneity, and adjusting processing parameters (pressing temperature, pressure, adhesive viscosity) for consistent fiber incorporation. Additionally, economic and environmental considerations—such as CF cost, energy use, emissions, and recyclability—require careful evaluation. Therefore, there is a clear scientific need to investigate how varying CF content affects bending strength, stiffness, density, and microstructural interactions in particleboards.
Although chopped CFRP fibers are relatively expensive, there are several application scenarios where the improvement in mechanical performance may justify the additional cost. High-performance particleboards used in load-bearing furniture elements, lightweight structural panels, or components for transportation and modular construction require mechanical properties that exceed those of conventional boards. Even moderate increases in bending strength and stiffness can enable material reduction, allow for thinner or lighter panels, and improve design safety margins. Furthermore, the rapid development of composite-recycling technologies has significantly increased the availability of low-cost recycled CFRP fibers, which are already being investigated as feasible reinforcement for engineered wood products. Therefore, the present study aims to evaluate the mechanical effects and feasibility of CFRP reinforcement as a first step toward assessing its cost–performance potential in specialized applications.
This study addresses this research gap by systematically examining the influence of CF content on pMDI-bonded single-layer particleboards. The main objective is to determine whether CF reinforcement can enhance mechanical performance while potentially reducing panel thickness or density. The hypothesis is that even low CF fractions can significantly improve bending strength and stiffness without replacing the bulk lignocellulosic fraction, providing insights into optimal fiber content, distribution, and resulting composite properties.
2. Materials and Methods
Single-layer particleboards were manufactured using industrial Scots pine (Pinus sylvestris L.) core-layer wood chips with an initial moisture content of approximately 5%. The particles were obtained from a single commercial supplier, and more than 80% of them corresponded to the fraction retained on a 2 mm sieve. The same batch of particles was used for all board variants to ensure consistency across experiments. While particle size and geometry can influence mechanical performance, all variants were produced from this uniform batch, ensuring that observed differences primarily result from carbon fiber reinforcement.
Polymeric methylene diphenyl diisocyanate (pMDI, 100% solid content), supplied by Wanhua Chemical Group Co. (Yantai, China), was used as the adhesive. This resin is commonly applied in the production of particleboards requiring zero formaldehyde emission (E0 class) and is also the preferred binder when incorporating poorly water-wettable raw materials, such as synthetic carbon fibers or agricultural residues (e.g., straw), due to its moisture-independent curing behavior and strong interaction with hydrophobic surfaces. The wood particles were bonded with an adhesive content of 10% (pMDI), given on a dry mass basis. The adhesive was applied by spraying, and uniformity was verified visually and by mass balance, ensuring adequate surface coverage. Synthetic carbon fibers were purchased as pre-chopped, with an average length of 7100 µm and diameter of 5 µm, without any additional surface treatment. The fibers were used as received, with moisture content verified prior to incorporation, approximately 0.5%–1.0%, and were randomly distributed within the mat to ensure isotropic reinforcement.
Six variants of single-layer particleboards were produced, corresponding to different carbon fiber contents: 0% (control board without carbon fibers), 10%, 20%, 30%, 40%, and 50% (ratio of carbon fibers to wood chips, e.g., 10/90, 20/80, etc., based on the oven-dry mass of wood particles), with three replicates per variant. Industrial wood chips, carbon fibers, and pMDI adhesive were blended in a laboratory mixer equipped with a bottom-mounted impeller (custom-built by OBRPPD, Czarna Woda, Poland). The mixer had a working volume of approximately 40 L and was designed to ensure effective agitation of low-bulk-density lignocellulosic materials. All furnish variants were mixed under identical conditions. Mixing was performed at approximately 20 rpm for about five minutes, which ensured adequate dispersion of the adhesive and minimized the risk of carbon fiber clustering. The relatively low rotational speed was selected to avoid excessive mechanical damage to the fibers while still providing sufficient shear to promote uniform distribution. For the control variant, only wood chips and pMDI adhesive were blended under the same mixing conditions. No paraffin or additional hydrophobic additives were used in any of the formulations.
The mat was formed in a 30 × 30 cm forming box, producing particleboard panels with final dimensions of approximately 32 × 32 cm after hot pressing. After mixing, the blended furnish was evenly distributed in the forming box and compacted using a stamp to achieve uniform thickness and density. The target density of the particleboards was 700 kg/m3 with a nominal thickness of 10 mm. The compacted mats were placed in a single-stage hydraulic press, using 10 mm thick pressing strips between the plates to ensure uniform board thickness and to prevent sticking. Pressing was carried out under controlled temperature, pressure, and time conditions (parameters shown in Table 1), optimized to ensure proper curing of the adhesive and effective integration of the carbon fibers with the wood chips.
Table 1.
Pressing parameters of boards for all variants.
The boards were conditioned under normal conditions (20 ± 2 °C, 65 ± 5% relative humidity) for 7 days before samples were taken to test selected physical and mechanical properties. Three boards were prepared for each variant to allow statistical analysis of the measured physical and mechanical properties.
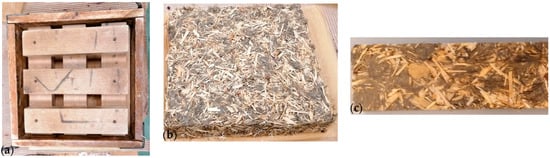
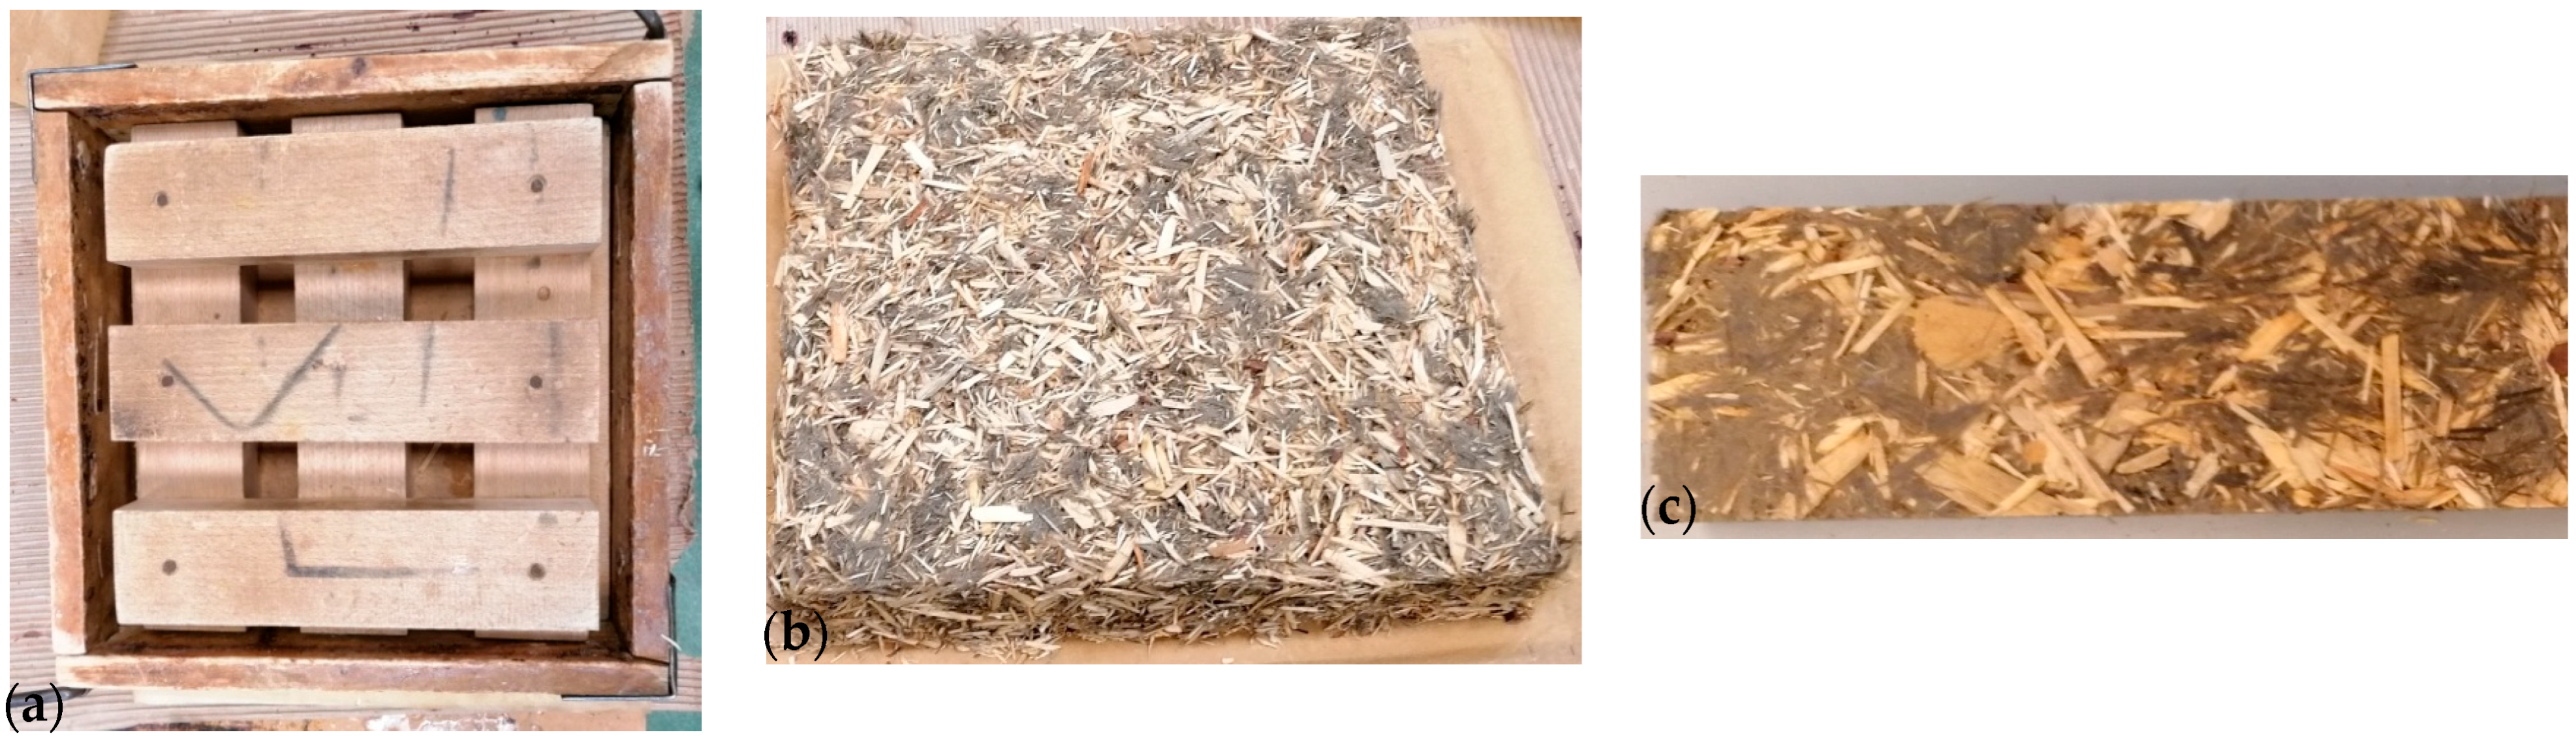
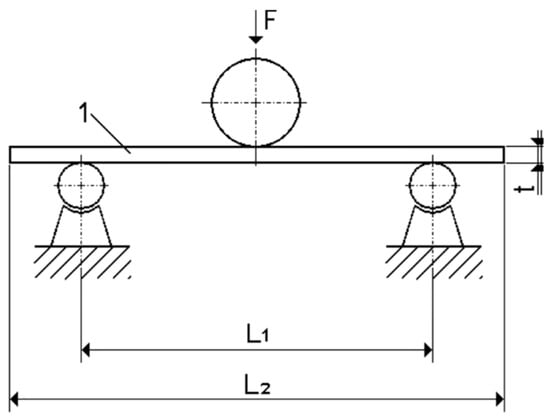
In Figure 1, the following are shown: the mat in the forming box covered with a platen (a); the mat after removal from the forming box (b); and the produced board variant containing 50% carbon fiber in the composition (c).
Figure 1.
Particleboard formation with carbon fibers: (a) mat in the forming box under the platen, (b) mat after removal, and (c) board with 50% carbon fiber.
2.1. Density Profile Across the Thickness
To determine the density distribution across the thickness, three samples (50 × 50 mm, 10 mm thick) were taken from each of the three boards produced per variant, with six variants in total, resulting in nine samples analyzed per variant using a DAX density profiler (GreCon, Alfeld, Germany) with a measurement step of 0.02 mm and a scanning speed of 0.05 mm/s. Test specimens for density profile measurements were cut randomly from each replicate board, without preferential selection of center or edge regions, to ensure representative sampling. No specimens were discarded, as no visible defects were observed in any of the panels.
2.2. Modulus of Elasticity (MOE) and Modulus of Rupture (MOR)
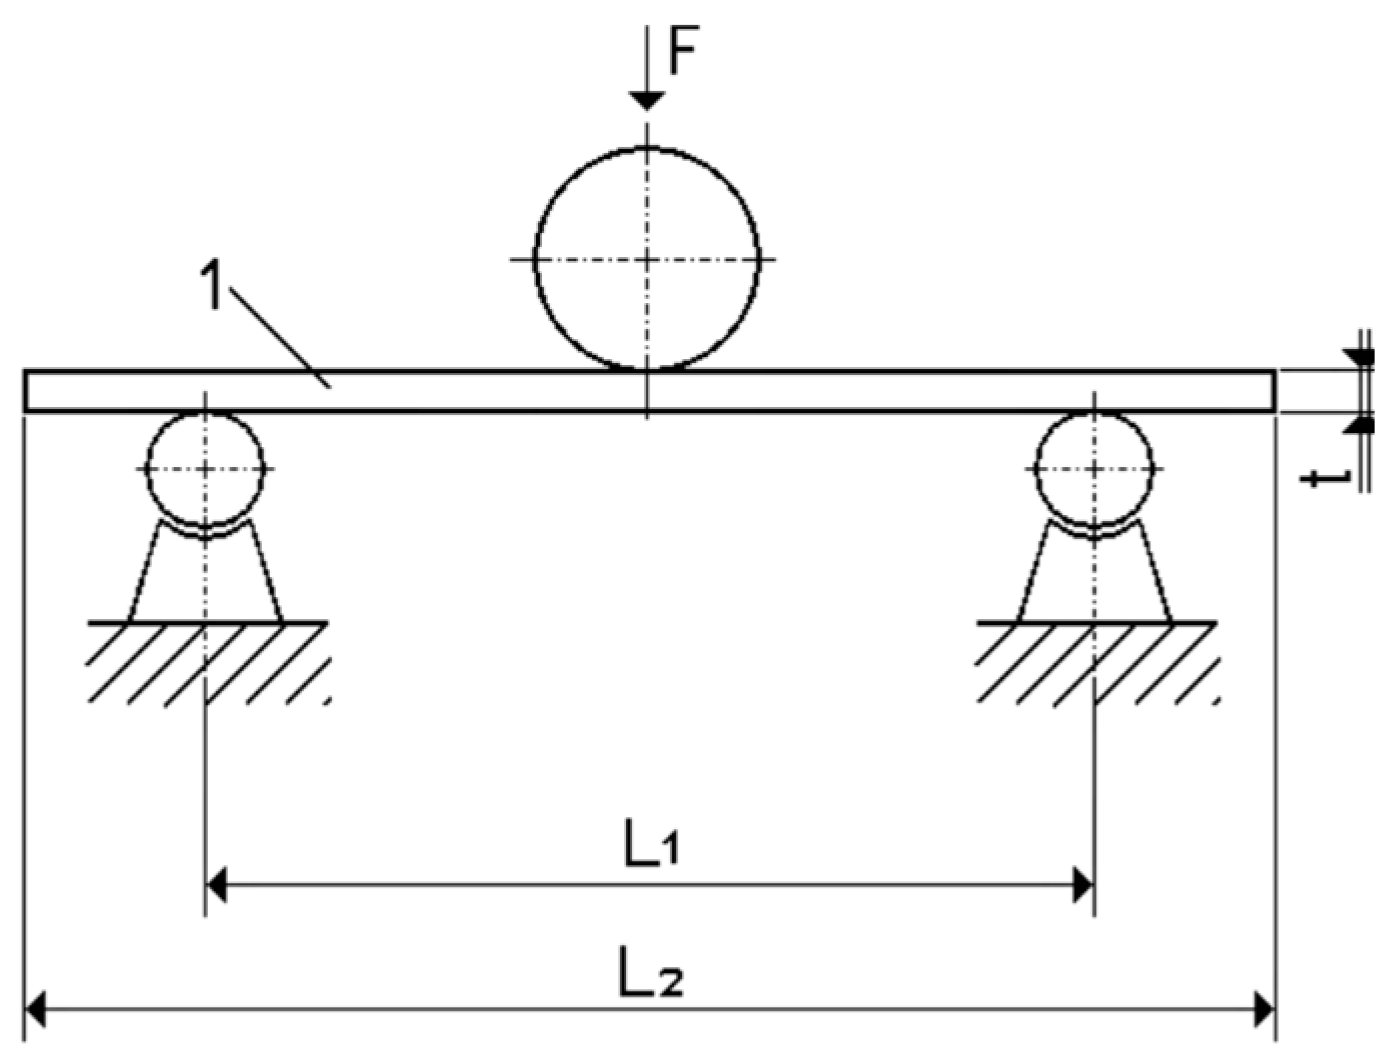
The mechanical tests were conducted using a custom-made universal testing machine built by the Research & Development Center for Wood-Based Panels Sp. z o.o. in Czarna Woda, Poland with a 2000 N load cell, certified and calibrated. Specimens were supported on steel rollers and tested at a displacement rate of 10 mm/min. The modulus of elasticity (MOE) and modulus of rupture (MOR) were determined according to PN-EN 310:1994 [41]. For each board variant, three boards were manufactured, and a total of ten test specimens were sampled from these boards. Six variants were produced in total. Samples were prepared according to standard dimensions for bending tests (50 × 300 × 10 mm) and were simply supported over a span of 200 mm. Specimens for bending tests were sampled randomly from each replicate board, without intentional selection of either central or peripheral regions. All specimens met visual quality criteria, and none were rejected due to defects, as no structural irregularities were present in the manufactured boards. The load was applied at midspan until failure (Fmax) occurred, as illustrated in Figure 2.
Figure 2.
Schematic of the specimen placement in the testing machine. 1—specimen, t—specimen thickness (10 mm), L1—support span (200 mm), L2—specimen length (300 mm), F—force application.
2.3. Screw-Holding Capacity
For each of the six board variants, three boards were manufactured, and a total of ten test specimens (50 × 50 × 10 mm) were sampled from these boards. Samples were taken randomly from each replicate panel, with no preferential sampling of center versus edge regions. No specimens were excluded from testing, as no manufacturing defects were identified in the panels. The specimens were tested in accordance with PN-EN 13446:2004 [42]. A 2 mm diameter pilot hole was drilled at the intersection of diagonals, and a screw was inserted protruding 3–5 mm above the surface. Samples were then clamped in the testing machine and loaded until failure (Fmax).
2.4. Statistical Analysis
Statistical analysis of the results was carried out using Statistica, version 13 (TIBCO Software Inc., Palo Alto, CA, USA). Analysis of variance (ANOVA) was applied (α = 0.05) to determine statistically significant differences between the factors. Mean values were compared using Tukey’s test at a significance level of α = 0.05.
3. Results and Discussion
3.1. Density Profile
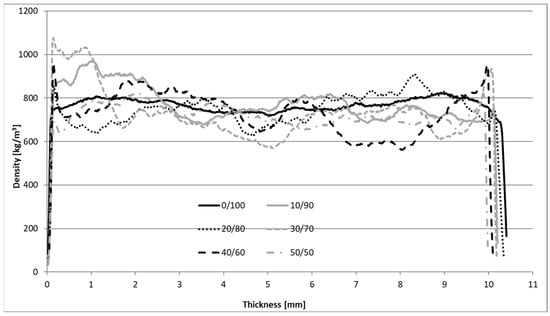
Figure 3 shows the density profiles of single-layer particleboards containing varying amounts of carbon fibers. The control board (0/100) exhibited the typical “U-shaped” density distribution for laboratory-pressed panels, with higher density in the surface layers (approximately 800 kg/m3) and lower density in the core (around 700–750 kg/m3). The addition of carbon fibers influenced the consolidation of the mat and the internal structure of the boards. At 10%–20% fiber content, the density distribution remained relatively uniform, although a slight increase in density near the surfaces was observed, suggesting that a moderate fiber content does not disrupt mat consolidation and allows effective bonding of wood particles.
Figure 3.
Typical density distribution of single-layer particleboards for different variants.
However, at higher fiber contents (≥30%), significant deviations from the standard profile were observed—boards exhibited pronounced density peaks near the surfaces (over 900–1000 kg/m3) and reduced density in the core (650–700 kg/m3). This distribution indicates uneven mat compaction, resulting from the lower compressibility and limited bonding ability of carbon fibers compared to wood particles. This phenomenon may also reflect the tendency of carbon fibers to cluster and mix non-uniformly with wood particles, leading to local variations in compaction.
The density distribution in particleboards depends on multiple factors, including mat compaction degree, resistance of material layers during pressing, pressing pressure and temperature, and the time required to reach the target thickness [43]. Since the only variable in this study was the carbon fiber content, the observed differences in density profiles can be mainly attributed to the high-speed mixer blending process and the effectiveness of adhesive distribution.
Overall, increasing the carbon fiber content led to greater heterogeneity in the density profile. For fiber contents up to 20%, the structure remained uniform and stable, whereas higher contents resulted in irregular compaction, potentially compromising the mechanical integrity of the boards. These results indicate that excessive carbon fiber addition may weaken the structural cohesion of the composite, despite the favorable mechanical properties of the fibers themselves.
3.2. Modulus of Elasticity and Modulus of Rupture
The mechanical properties of the single-layer particleboards are summarized in Table 2, and the results of the analysis of variance are shown in Table 3. The addition of carbon fibers significantly influenced the bending properties of the boards (p < 0.05). The highest modulus of rupture (MOR) was observed for the 10/90 variant, which reached an average value of 28.1 N/mm2—approximately 26% higher than that of the control board (22.3 N/mm2). This improvement indicates that a small addition of carbon fibers effectively enhances load transfer and stiffness within the composite structure. Carbon fibers act as micro-reinforcements, forming load-transferring bridges between wood particles, thereby enhancing the structural integrity of the composite [44,45].
Table 2.
Mechanical properties of single layer particleboards.
Table 3.
Analysis of variance for single layer panels regarding the carbon fiber content.
The observed reductions in MOE and MOR at higher carbon fiber contents can be attributed to microstructural effects such as fiber agglomeration, limited wettability, and the formation of fiber clusters, which can hinder effective stress transfer within the composite matrix. Carbon fibers are known to have inherently poor wettability due to the lack of active functional groups on their surface, which negatively affects interfacial adhesion and load transfer in polymer composites unless surface modifications are applied. Surface treatments and electrically assisted wetting techniques have been shown to improve wettability and enhance interfacial bonding, leading to notable improvements in interfacial shear strength and overall mechanical performance of carbon fiber composites [46].
Similar effects of incomplete impregnation and uneven fiber distribution have been reported in composite systems, where localized regions with poor fiber–matrix interaction or voids lead to stress concentrations and reduced mechanical performance. Porosity and void formation during impregnation significantly degrade matrix-dominated properties such as bending and interlaminar shear strength, further supporting our interpretation of mechanical trends despite the absence of direct microscopic imaging in the present study [47].
In the board, a more uniform stress distribution within the structure is observed, along with efficient interfacial stress transfer due to the difference in modulus of elasticity between wood and carbon fibers, which, when evenly dispersed, increase resistance to crack initiation [48].
A further increase in carbon fiber content, however, resulted in a gradual decline in MOR, with the lowest value recorded for the 50/50 variant (18.1 N/mm2). This trend suggests that excessive fiber content leads to undesired phenomena such as fiber agglomeration, limited wettability, and reduced effective wood–adhesive–fiber bonding [49,50]. Moreover, studies on wood–polymer composites and hybrid panels indicate that increasing the fibrous phase above a critical threshold results in a decline in mechanical performance due to reduced cohesion in the lignocellulosic matrix [44,51,52]. In such cases, partial recovery of mechanical properties can be achieved through surface modification of the fibers (e.g., oxidation, silanization) or by adjusting their incorporation method into the matrix. Excess synthetic fibers may generate agglomerates, voids, and local stress concentrations, as well as hinder adhesive penetration [53,54]. Consequently, material cohesion and macroscopic load-transfer efficiency are compromised.
According to Drouet [55], for medium-density particleboards (500–750 kg/m3, thickness 8–25 mm), the modulus of rupture (MOR) ranges from 15 to 25 N/mm2. Niemz [56] reports lower values (13–18 N/mm2) for boards of 680–750 kg/m3 density and thickness ≥13 mm, while PN-EN 312:2011 [57] specifies MOR values of 12.5–22 N/mm2 for boards 6–13 mm thick. The experimental results for the 10/90 variant exceed the upper limits of both literature data and normative requirements, confirming the beneficial effect of moderate carbon fiber addition. The control board (0/100) also approached the upper normative limit, indicating high-quality raw material and production processes.
Statistical analysis of the modulus of elasticity (MOE) results (Table 3) showed a significant effect of carbon fiber content on board stiffness (p = 0.002446). Unlike MOR, which is highly influenced by local defects and surface quality, MOE reflects the global rigidity and elastic response of the entire structure. The highest average MOE was recorded for the 10/90 variant (3590 N/mm2), corresponding to an increase of approximately 19% compared to the control board (3021 N/mm2). This indicates that a small addition of carbon fibers enables efficient stress transfer between wood particles [44,48]. Carbon fibers, characterized by a very high modulus of elasticity (~230–240 GPa), enhance material resistance to elastic deformation, acting as reinforcement within the wood-based matrix. When the carbon fiber content exceeded 20%, a systematic decrease in MOE was observed. The lowest MOE (2722 N/mm2) was measured for the 50/50 variant. This decline is not solely due to reduced effective density but also results from weakened interfacial cohesion and limited fiber wettability by the adhesive [49]. Despite their high stiffness, carbon fibers cannot contribute effectively to load transfer when poorly anchored in the matrix, leading to local microcracks and structural discontinuities [54]. Such behavior is typical for composites with high reinforcement fractions, where the effective reinforcement saturation threshold is exceeded. In terms of stiffness, the MOE enhancement observed in the present study (approximately +19% for the 10/90 variant) also aligns with previously reported data. Charlet et al. [53] documented a 20%–30% increase in MOE in wood–polymer composites reinforced with carbon or flax fibers at fiber loadings between 8% and 12%, after which the stiffness began to decline due to fiber clustering and reduced bonding quality.
Incorporating carbon fibers into particleboard structure affects not only stress transfer but also deformation behavior under load. At low fiber contents (<15%), a “micro-bridging” effect is observed, where fibers act as local reinforcements, limiting bending and preventing micro-slips between wood particles [52]. At fiber contents above 30%, structural segmentation occurs, with fibers forming clusters that hinder adhesive flow and uniform compaction during pressing [51]. Consequently, despite the high potential of carbon fibers, reinforcement efficiency depends on fiber dispersion, orientation, and interfacial bonding quality. Improvements can be achieved via surface modification (e.g., oxidation, silanization) or use of adhesives with higher polarity [49,53].
The measured MOE values fall within the range reported for medium-density particleboards (2500–4500 MPa) [54] and comply with [58] requirements (1800–3350 MPa). Values for the 10/90 variant exceed the upper normative limit, confirming the positive effect of moderate fiber addition on stiffness. For comparison, Niemz [56] reports 2200 MPa for boards of similar density and thickness, indicating a 40%–60% improvement due to effective structural reinforcement. It is also worth noting that, in addition to carbon fiber addition, other unexamined factors had a substantial influence on MOR and MOE, accounting for 48.5% and 64.1%, respectively (Table 3).
3.3. Screw-Holding Capacity
Analysis of variance of the screw withdrawal strength results (Table 3) indicated that carbon fiber content had a significant effect (p = 0.000678). Mean values ranged from 146.5 N/mm (50/50 variant) to 223.8 N/mm (30/70 variant), while the control board (0/100) reached 201.6 N/mm. The overall trend—improved resistance at moderate fiber content (20%–30%) and a decline at higher levels (≥40%–50%)—can be attributed to a combination of two mechanisms: local reinforcement around the screw shank due to fiber dispersion, and reduced cohesion of wood chips at excessive fiber content (agglomeration, increased porosity, and insufficient adhesive wetting). The observed decrease in screw withdrawal resistance (SWR) at carbon fiber contents ≥ 40% can be attributed to microstructural effects. High fiber content may induce local density variations and disrupt the continuity of the wood–adhesive matrix, creating zones of reduced cohesion. Additionally, excessive fibers can hinder adhesive penetration and alter short fiber orientation, limiting the effective contact area for screw threads. Similar trends have been reported in wood–polymer composites, where high reinforcement fractions negatively affected interfacial bonding and fastener performance [58].
These trends align with recent studies on synthetic fiber-reinforced wood, where moderate additions of carbon or glass fibers improved withdrawal strength, but excessive reinforcement weakened anchorage and reduced point load capacity [59]. Similar observations were reported for carbon fiber-reinforced wood elements. Saad et al. [48] emphasize that reinforcement efficiency strongly depends on the quality of adhesion between the fiber phase and the wood-based matrix.
In particleboards with short (chopped) fibers, fiber length and dispersion critically affect mechanical performance. Uneven distribution creates local weak zones, reducing screw withdrawal resistance. In the present study, the decrease in screw holding strength at fiber contents above 30% likely resulted from lower effective structural density and insufficient fiber wetting by the binder. Surface modification of carbon fibers, through chemical or plasma treatments, has been shown to increase roughness and introduce functional groups that enhance adhesion, thereby improving mechanical joint strength and stress transfer [60]. Applying such modified fibers could mitigate the observed strength reduction at higher fiber fractions.
Furthermore, Sayam et al. [61] report that hierarchical composites containing both long and short fibers can achieve synergistic reinforcement while maintaining structural integrity. Future research could explore hybrid reinforcements (e.g., combining carbon and glass fibers) to enhance screw withdrawal resistance without compromising particleboard cohesion [62]. It should also be noted that unexamined factors contributed 58.1% of the variance in screw withdrawal strength, whereas carbon fiber addition accounted for 41.9% (Table 3).
It should be noted that the present study has several limitations. Only a single type of carbon fiber with fixed diameter and length was used, and no surface treatment was applied, which may have affected interfacial adhesion and stress transfer. Additionally, chemical characterization of the fiber–matrix interface was not performed, and certain physical properties such as water absorption and thickness swelling were not evaluated. Future research should explore alternative fiber types, surface modifications, and comprehensive testing of both mechanical and physical properties to fully understand and optimize the performance of CFRP-reinforced particleboards.
From a practical perspective, the results obtained for the 10% CF variant need to be considered in light of economic and technological constraints. Although this reinforcement level produced the most favorable balance between mechanical improvements and board density, the cost of carbon fibers remains significantly higher than that of conventional lignocellulosic raw materials. A preliminary economic estimation indicates that the 26% increase in MOR and the 19% improvement in MOE may not fully offset the cost of CF at current market prices, particularly for low-margin particleboard production. Furthermore, industrial implementation would require optimized mixing systems to ensure homogeneous fiber dispersion; otherwise, agglomeration and local weakening of the board could occur, as already suggested by the microstructural observations. These factors imply that the applicability of carbon fiber reinforcement may be limited to high-performance or specialty boards, unless future reductions in CF cost or advances in fiber surface treatments and dispersion technologies make large-scale use more feasible.
4. Conclusions
The study demonstrates that the addition of carbon fibers (CF) influences the structure and mechanical performance of single-layer particleboards. Key conclusions are:
- Structural effect: Incorporation of CF alters the density profile, producing a more heterogeneous board structure.
- Mechanical enhancement at moderate content: A 10% CF addition yielded the highest improvements, with modulus of rupture (MOR) increasing by 26% (from 22.3 to 28.1 N/mm2) and modulus of elasticity (MOE) increasing by 19% (from 3021 to 3590 N/mm2), meeting the PN-EN 312 requirements for P7-grade boards.
- Limitation of excessive CF content: Contents above 30% reduce mechanical performance due to uneven fiber distribution, agglomeration, and weakened interfacial adhesion.
- Application potential and further research: CF reinforcement can be considered for high-performance or specialized particleboards, but economic feasibility and industrial-scale fiber dispersion remain critical challenges. Future work should optimize fiber content and distribution, explore surface treatments to improve adhesion, and assess cost–performance and environmental impacts.
Author Contributions
Conceptualization, I.B. and M.B.; methodology, I.B.; software, I.B.; validation, I.B.; formal analysis, I.B.; investigation, I.B. and M.B.; data curation, I.B.; writing—original draft preparation, I.B. and P.B.; writing—review and editing, I.B. and P.B.; visualization, I.B.; supervision, I.B.; project administration, I.B. All authors have read and agreed to the published version of the manuscript.
Funding
This research received no external funding.
Institutional Review Board Statement
Not applicable.
Informed Consent Statement
Not applicable.
Data Availability Statement
The raw data supporting the conclusions of this article will be made available by the authors on request.
Conflicts of Interest
The authors declare no conflicts of interest.
References
- Food and Agriculture Organization of the United Nations (FAO). Forestry–FAO. FAO Website. Available online: https://www.fao.org/forestry (accessed on 2 November 2025).
- Chaharmahali, M.; Tajvidi, M.; Kazemi, S. Mechanical properties of wood plastic composite panels made from waste fiberboard and particleboard. Polym. Compos. 2008, 29, 606–610. [Google Scholar] [CrossRef] [Scilit]
- Estrada-Monje, A.; Alonso-Romero, S.; Zitzumbo-Guzmán, R.; Estrada-Moreno, I.A.; Zaragoza-Contreras, E.A. Thermoplastic starch-based blends with improved thermal and thermomechanical properties. Polymers 2021, 13, 4263. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Maksymiuk, G.; Jeżo, A.; Rižikovs, J. Selected physical and mechanical properties of particleboards manufactured with addition of Betula bark post-extraction residues. Eur. J. Wood Prod. 2024, 82, 1981–1992. [Google Scholar] [CrossRef] [Scilit]
- Maulana, M.I.; Lubis, M.A.R.; Febrianto, F.; Hua, L.S.; Iswanto, A.H.; Antov, P.; Kristak, L.; Mardawati, E.; Sari, R.K.; Zaini, L.H.; et al. Environmentally friendly starch-based adhesives for bonding high-performance wood composites: A review. Forests 2022, 13, 1614. [Google Scholar] [CrossRef] [Scilit]
- Han, G.; Deng, J.; Zhang, S.; Bicho, P.; Wu, Q. Effect of steam explosion treatment on characteristics of wheat straw. Ind. Crops Prod. 2010, 31, 28–33. [Google Scholar] [CrossRef] [Scilit]
- Tabarsa, T.; Jahanshahi, S.; Ashori, A. Mechanical and physical properties of wheat straw boards bonded with a tannin modified phenol-formaldehyde adhesive. Compos. B Eng. 2011, 42, 176–180. [Google Scholar] [CrossRef] [Scilit]
- Halvarsson, S.; Edlund, H.; Norgren, M. Manufacture of high-performance rice-straw fiberboards. Ind. Eng. Chem. Res. 2009, 49, 1428–1435. [Google Scholar] [CrossRef] [Scilit]
- Li, X.; Cai, Z.; Winandy, J.E.; Basta, A.H. Selected properties of particleboard panels manufactured from rice straws of different geometries. Bioresour. Technol. 2010, 101, 4662–4666. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Ghalehno, M.D.; Nazerian, M.; Bayatkashkooli, A. Influence of utilization of bagasse in surface layer on bending strength of three-layer particleboard. Eur. J. Wood Prod. 2011, 69, 533–535. [Google Scholar] [CrossRef] [Scilit]
- Paridah, M.T.; Juliana, A.H.; El-Shekeil, Y.A.; Jawaid, M.; Alothman, O.Y. Measurement of mechanical and physical properties of particleboard by hybridization of kenaf with rubberwood particles. Meas. J. Int. Meas. Confed. 2014, 56, 70–80. [Google Scholar] [CrossRef] [Scilit]
- Papadopoulos, A.N.; Hill, C.A.S.; Gkaraveli, A.; Ntalos, G.A.; Karastergiou, S.P. Bamboo chips (Bambusa vulgaris) as an alternative lignocellulosic raw material for particleboard manufacture. Holz Roh Werkst. 2004, 62, 36–39. [Google Scholar] [CrossRef] [Scilit]
- Khedari, J.; Nankongnab, N.; Hirunlab, J.; Teekasap, S. New low-cost insulation particleboards from mixture of durian peel and coconut coir. Build. Environ. 2004, 39, 59–65. [Google Scholar] [CrossRef] [Scilit]
- Auriga, R.; Borysiuk, P.; Gumowska, A.; Smulski, P. Influence of apple wood waste from the annual care cut on the mechanical properties of particleboards. Ann. Warsaw Univ. Life Sci. For. Wood Technol. 2019, 105, 47–53. [Google Scholar] [CrossRef] [Scilit]
- Sekaluvu, L.; Tumutegyereize, P.; Kiggundu, N. Investigation of factors affecting the production and properties of maize cob-particleboards. Waste Biomass Valoriz. 2014, 5, 27–32. [Google Scholar] [CrossRef] [Scilit]
- Papadopoulou, E.; Chrysafi, I.; Karidi, K.; Mitani, A.; Bikiaris, D.N. Particleboards with recycled material from hemp-based panels. Materials 2024, 17, 139. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Nikvash, N.; Kraft, R.; Kharazipour, A.; Euring, M. Comparative properties of bagasse, canola and hemp particle boards. Eur. J. Wood Prod. 2010, 68, 323–327. [Google Scholar] [CrossRef] [Scilit]
- Papadopoulos, A.N.; Hague, J.R.B. The potential for using flax (Linum usitatissimum L.) shiv as a lignocellulosic raw material for particleboard. Ind. Crops Prod. 2003, 17, 143–147. [Google Scholar] [CrossRef] [Scilit]
- Alma, M.H.; Kalaycioglu, H.; Bektas, I.; Tutus, A. Properties of cotton carpel-based particleboards. Ind. Crops Prod. 2005, 22, 141–149. [Google Scholar] [CrossRef] [Scilit]
- Nemli, G.; Demirel, S.; Gümüşkaya, E.; Aslan, M.; Acar, C. Feasibility of incorporating waste grass clippings (Lolium perenne L.) in particleboard composites. Waste Manag. 2009, 29, 1129–1131. [Google Scholar] [CrossRef] [Scilit]
- Taha, I.; Elkafafy, M.S.; El Mously, H. Potential of utilizing tomato stalk as raw material for particleboards. Ain Shams Eng. J. 2018, 9, 1457–1464. [Google Scholar] [CrossRef] [Scilit]
- Guntekin, E.; Karakus, B. Feasibility of using eggplant (Solanum melongena) stalks in the production of experimental particleboard. Ind. Crops Prod. 2008, 27, 354–358. [Google Scholar] [CrossRef] [Scilit]
- Gürü, M.; Tekeli, S.; Bilici, İ. Manufacturing of urea formaldehyde-based composite particle board from almond shell. Mater. Des. 2006, 27, 1148–1151. [Google Scholar] [CrossRef] [Scilit]
- Guler, C.; Copur, Y.; Tascioglu, C. The manufacture of particleboards using mixture of peanut hull (Arachis hypogaea L.) and European black pine (Pinus nigra Arnold) wood chips. Bioresour. Technol. 2008, 99, 2893–2897. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Bekalo, S.A.; Reinhardt, H.-W. Fibers of coffee husk and hulls for the production of particleboard. Mater. Struct. 2010, 43, 1049–1060. [Google Scholar] [CrossRef] [Scilit]
- Nemli, G.; Kirci, H.; Serdar, B.; Ay, N. Suitability of kiwi (Actinidia sinensis Planch.) prunings for particleboard manufacturing. Ind. Crops Prod. 2003, 17, 39–46. [Google Scholar] [CrossRef] [Scilit]
- Auriga, R.; Auriga, A.; Borysiuk, P.; Wilkowski, J.; Fornalczyk, O.; Ochmian, I. Lignocellulosic biomass from grapevines as raw material for particleboard production. Polymers 2022, 14, 2483. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Borysiuk, P.; Jenczyk-Tolloczko, I.; Auriga, R.; Kordzikowski, M. Sugar beet pulp as raw material for particleboard production. Ind. Crops Prod. 2019, 141, 111829. [Google Scholar] [CrossRef] [Scilit]
- Yalinkilic, M.K.; Imamura, Y.; Takahashi, M.; Kalaycioglu, H.; Nemli, G.; Demirci, Z.; Ozdemir, T. Biological, physical and mechanical properties of particleboard manufactured from waste tea leaves. Int. Biodeterior. Biodegrad. 1998, 41, 75–84. [Google Scholar] [CrossRef] [Scilit]
- Borysiuk, P.; Dziurka, D.; Jabłoński, M.; Kundzewicz, A.; Zbieć, M. Glass-fiber reinforced chipboard. Ann. Warsaw Univ. Life Sci. For. Wood Technol. 2007, 61, 67–70. [Google Scholar]
- Čabalová, I.; Krilek, J.; Bubeníková, T.; Ružiak, I.; Nemec, M.; Lee, S.H.; Lubis, M.A.R.; Darabošová, A.; Mancel, V.; Kristak, L.; et al. Utilization of waste tire and rubber from automobiles in the manufacturing of particleboards and evaluation of its properties. Eur. J. Wood Prod. 2025, 83, 67. [Google Scholar] [CrossRef] [Scilit]
- Hermawan, A.; Ohuchi, T.; Fujimoto, N.; Murase, Y. Manufacture of composite board using wood prunings and waste porcelain stone. J. Wood Sci. 2009, 55, 74–79. [Google Scholar] [CrossRef] [Scilit]
- Zhang, H.; Zheng, N.; Xing, T.; Zhang, G.; Cao, D.; Bai, Y.; Wang, S.; Zuo, D.; Liu, H.; Li, S.; et al. Study on the characteristics of glass fiber-reinforced polymers from recycled wind turbine blades as reinforcement in particleboard. Polym. Compos. 2024, 45, 10865–10879. [Google Scholar] [CrossRef] [Scilit]
- Iswanto, A.H.; Febriansyah, R.; Tanjung, Y.A.; Nainggolan, A.; Nabila, N.; Hakim, L.; Sucipto, T.; Sutiawan, J.; Aristri, M.A.; Rogoziński, T.; et al. Development and characterization of novel particleboard panels manufactured from organic waste with fiberglass reinforcement. Results Eng. 2025, 27, 105893. [Google Scholar] [CrossRef] [Scilit]
- Bakalarz, M.; Kossakowski, P. Mechanical properties of laminated veneer lumber beams strengthened with CFRP sheets. Arch. Civ. Eng. 2019, 65, 57–66. [Google Scholar] [CrossRef] [Scilit]
- Rescalvo, F.J.; Duriot, R.; Pot, G.; Gallego, A.; Denaud, L. Enhancement of bending properties of Douglas-fir and poplar laminate veneer lumber (LVL) beams with carbon and basalt fibers reinforcement. Constr. Build. Mater. 2020, 263, 120185. [Google Scholar] [CrossRef] [Scilit]
- Wang, Y.; Tang, Q.; Chen, X.; Luo, X.; Zhang, F.; Zhou, G.; Zhang, J.; Zhang, L.; Meng, Y.; Ren, Y.; et al. Performance evaluation of carbon fiber fabric-reinforced formaldehyde-free high-strength plywood. Polymers 2024, 16, 2637. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Łukawski, D.; Lekawa-Raus, A.; Lisiecki, F.; Koziol, K. Towards the development of superhydrophobic carbon nanomaterial coatings on wood. Prog. Org. Coat. 2018, 125, 23–31. [Google Scholar] [CrossRef] [Scilit]
- Łukawski, D.; Dudkowiak, A.; Janczak, D.; Lekawa-Raus, A. Preparation and applications of electrically conductive wood layered composites. Compos. A Appl. Sci. Manuf. 2019, 127, 105656. [Google Scholar] [CrossRef] [Scilit]
- Łukawski, D.; Hochmańska-Kaniewska, P.; Janiszewska-Latterini, D.; Lekawa-Raus, A. Functional materials based on wood, carbon nanotubes, and graphene: Manufacturing, applications, and green perspectives. Wood Sci. Technol. 2023, 57, 989–1037. [Google Scholar] [CrossRef] [Scilit]
- PN-EN 310:1994; Wood-Based Panels–Determination of Bending Strength and Modulus of Elasticity in Bending. Polish Committee for Standardization: Warsaw, Poland, 1994.
- PN-EN 13446:2004; Wood-Based Panels–Determination of Screw Withdrawal Resistance. Polish Committee for Standardization: Warsaw, Poland, 2004.
- Boruszewski, P.; Borysiuk, P.; Mamiński, M.; Nicewicz, D. Przewodnik do Ćwiczeń z Podstaw Technologii Tworzyw Drzewnych; Wydawnictwo SGGW: Warszawa, Poland, 2013. [Google Scholar]
- Núñez-Decap, M.; Barra-Rodríguez, Y.; Opazo-Carlsson, C.; Moya-Rojas, B.; Vidal-Vega, M.; Opazo-Vega, A. Use of carbon and basalt fibers with adhesives to improve physical and mechanical properties of plywood. Appl. Sci. 2022, 12, 5114. [Google Scholar] [CrossRef] [Scilit]
- Saal, K.; Kallakas, H.; Tuhkanen, E.; Just, A.; Rohumaa, A.; Kers, J.; Kalamees, T.; Lohmus, R. Fiber-reinforced plywood: Increased performance with less raw material. Materials 2024, 17, 3218. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Hakim, I.; Donaldson, S.; Meyendorf, N.; Browning, C. Porosity Effects on Interlaminar Fracture Behavior in Carbon Fiber-Reinforced Polymer Composites. Mater. Sci. Appl. 2017, 8, 170–187. [Google Scholar] [CrossRef]
- Chen, X.; Wen, K.; Wang, C.; Cheng, S.; Wang, S.; Ma, H.; Tian, H.; Zhang, J.; Li, X.; Shao, J. Enhancing mechanical strength of carbon fiber-epoxy interface through electrowetting of fiber surface. Compos. Part B Eng. 2022, 234, 109751. [Google Scholar] [CrossRef] [Scilit]
- Saad, K.; Lengyel, A. Strengthening timber structural members with CFRP and GFRP: A state-of-the-art review. Polymers 2022, 14, 2381. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Khan, T.A.; Gupta, A.; Jamari, S.S.; Jose, R.; Nasir, M.; Kumar, A. Synthesis and characterization of carbon fibers and their application in wood composites. BioResources 2013, 8, 4171–4184. [Google Scholar] [CrossRef] [Scilit]
- Khan, T.A.; Gupta, A.; Jamari, S.S.; Nasir, M.; Jang, S.; Kim, H.J.; Asim, M. Synthesis of micro carbonaceous material by pyrolysis of rubber wood and its effect on properties of urea-formaldehyde (UF) resin. Int. J. Adhes. Adhes. 2020, 99, 102589. [Google Scholar] [CrossRef] [Scilit]
- Pędzik, M.; Auriga, R.; Kristak, L.; Antov, P.; Rogoziński, T. Physical and mechanical properties of particleboard produced with addition of walnut (Juglans regia L.) wood residues. Materials 2022, 15, 1280. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Ramesh, M.; Rajeshkumar, L.; Sasikala, G.; Balaji, D.; Saravanakumar, A.; Bhuvaneswari, V.; Bhoopathi, R. A critical review on wood-based polymer composites: Processing, properties, and prospects. Polymers 2022, 14, 589. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Charlet, K.; Jernot, J.-P.; Gomina, M.; Bizet, L.; Breard, J. Mechanical properties of flax fibers and of the derived unidirectional composites. J. Compos. Mater. 2010, 44, 2887–2896. [Google Scholar] [CrossRef] [Scilit]
- Hernandez-Estrada, E.; Müssig, J.; Hughes, M. The impact of fibre processing on the mechanical properties of epoxy matrix composites and wood-based particleboard reinforced with hemp (Cannabis sativa L.) fibre. J. Mater. Sci. 2022, 57, 1738–1754. [Google Scholar] [CrossRef] [Scilit]
- Drouet, T. Technologia Płyt Wiórowych [Technology of Particleboards]; Wydawnictwo SGGW: Warsaw, Poland, 1992. [Google Scholar]
- Niemz, P. Physik des Holzes und der Holzwerkstoffe; DRW-Verlag: Leinfelden-Echterdingen, Germany, 1993. [Google Scholar]
- PN-EN 312:2011; Particleboards–Specifications. Polish Committee for Standardization: Warsaw, Poland, 2011.
- Perçin, O.; Uzun, O. Screw withdrawal strength of heat-treated and laminated veneer lumber reinforced with carbon and glass fibers. BioResources 2022, 17, 2486–2500. [Google Scholar] [CrossRef] [Scilit]
- Durmaz, S.; Erdil, Y.Z.; Avcı, E. Screw withdrawal resistance and surface roughness of woven carbon and glass fiber-reinforced wood plastic composites. BioResources 2020, 15, 1894–1903. [Google Scholar] [CrossRef] [Scilit]
- Peng, X.; Wu, Y.; Wei, Z. Research progress on the surface modification of carbon fiber. RSC Adv. 2024, 14, 4043–4064. [Google Scholar] [CrossRef] [PubMed]
- Sayam, A.; Rahman, A.N.M.M.; Rahman, M.S.; Smiriti, S.; Ahmed, F.; Rabbi, M.F.; Hossain, M.; Faruque, M.O. A review on carbon fiber-reinforced hierarchical composites: Mechanical performance, manufacturing process, structural applications and allied challenges. Carbon Lett. 2022, 32, 1173–1205. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Hayne, D.J.; Singleton, M.; Patterson, B.A.; Knorr, D.B.; Stojcevski, F.; Henderson, L.C. Carbon fiber surface treatment for improved adhesion and performance of polydicyclopentadiene composites synthesized by ring opening metathesis polymerization. Compos. Commun. 2024, 47, 101872. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2025 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license (https://creativecommons.org/licenses/by/4.0/).