-
Intelligent Non-Destructive Evaluation of Additively Manufactured Metal Parts: From Advanced Inspections to Data-Driven Quality Predictions -
Degradation and Long-Term Response Evaluation of Polymeric Components Produced by Additive Manufacturing -
Inverse Thermal Process Design for Interlayer Temperature Control in Wire-Directed Energy Deposition Using Physics-Informed Neural Networks -
Drilling Temperature and Cutting Force Analysis in Additive-Modified CFRP Composites
Journal Description
Journal of Manufacturing and Materials Processing
is an international, peer-reviewed, open access journal on the scientific fundamentals and engineering methodologies of manufacturing and materials processing published monthly online by MDPI.
- Open Access— free for readers, with article processing charges (APC) paid by authors or their institutions.
- High Visibility: indexed within Scopus, ESCI (Web of Science), Inspec, CAPlus / SciFinder, Ei Compendex and other databases.
- Journal Rank: JCR - Q1 (Engineering, Mechanical) / CiteScore - Q1 (Mechanical Engineering)
- Rapid Publication: manuscripts are peer-reviewed and a first decision is provided to authors approximately 13.7 days after submission; acceptance to publication is undertaken in 2.9 days (median values for papers published in this journal in the first half of 2026).
- Recognition of Reviewers: reviewers who provide timely, thorough peer-review reports receive vouchers entitling them to a discount on the APC of their next publication in any MDPI journal, in appreciation of the work done.
- Journal Cluster of Mechanical Manufacturing and Automation Control: Aerospace, Automation, Drones, Journal of Manufacturing and Materials Processing, Machines, Robotics and Technologies.
Impact Factor:
4.0 (2025);
5-Year Impact Factor:
4.0 (2025)
Latest Articles
Influence of Laser Parameters on the Activation of Cr2O3-Doped ZTA Ceramics for Selective Electroless Copper Plating in the Manufacture of 3D Ceramic Circuit Carriers
J. Manuf. Mater. Process. 2026, 10(9), 345; https://doi.org/10.3390/jmmp10090345 - 7 Sep 2026
Abstract
►
Show Figures
Due to the superior thermal, mechanical and chemical properties of ceramics, metallized ceramics are widely used as circuit carriers and interconnect devices, wherever standard polymer-based circuit boards come to their limits. 2D metallization represents the current state of the art. The metallization of
[...] Read more.
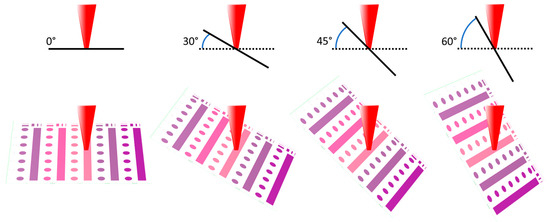
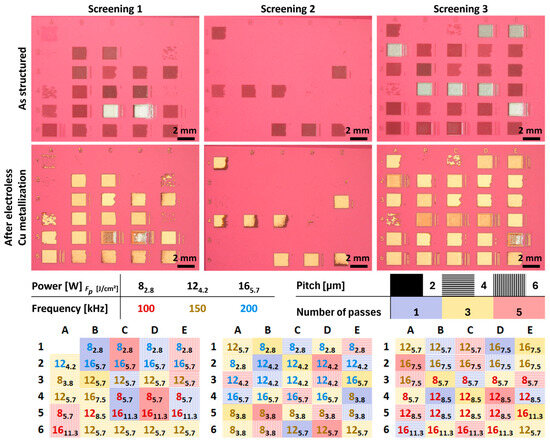
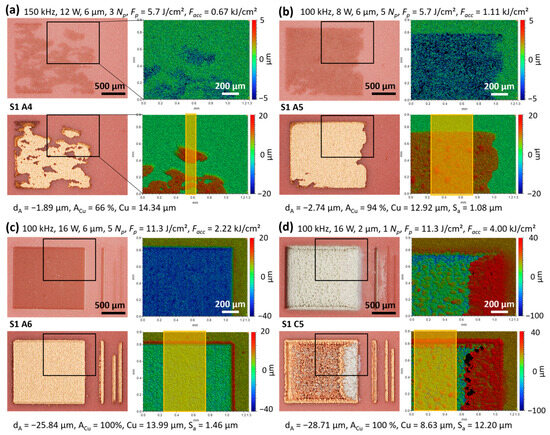
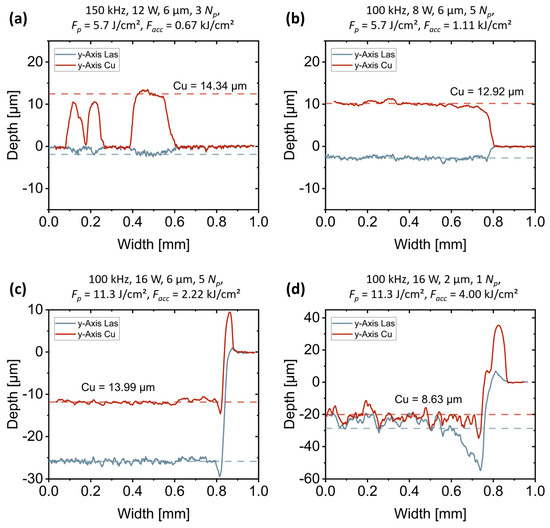
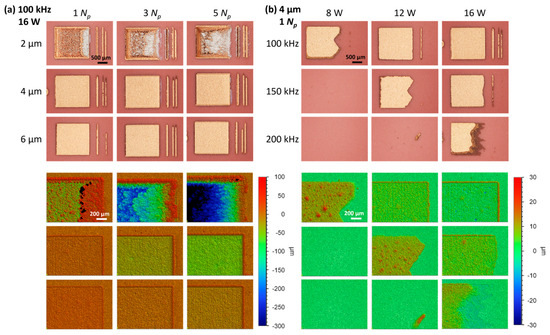
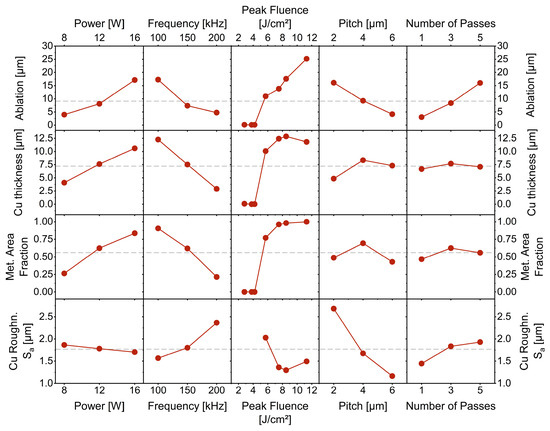
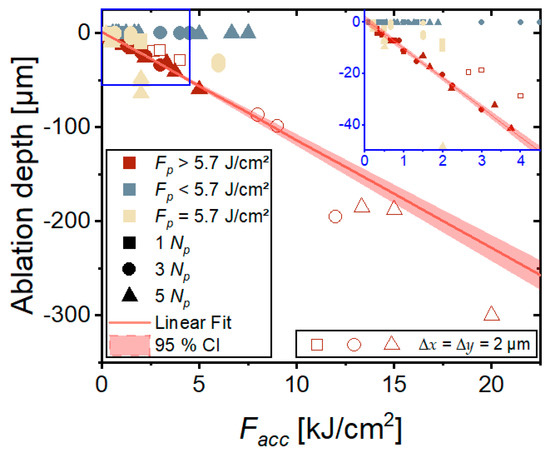
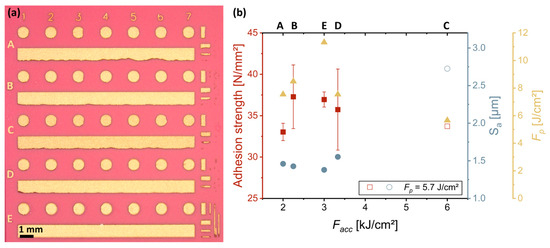
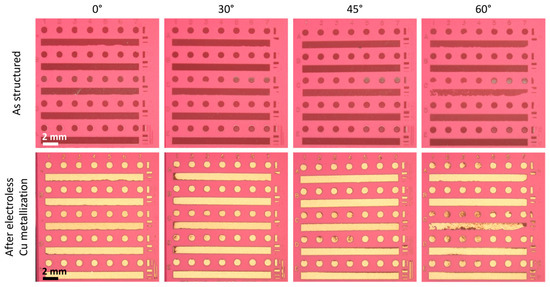
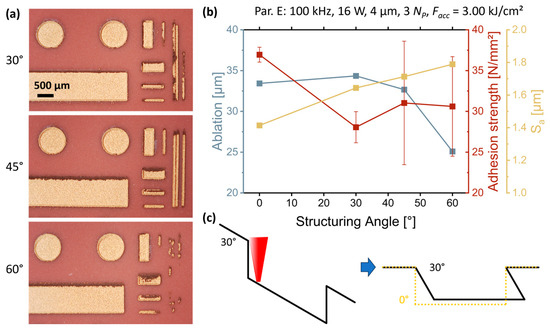
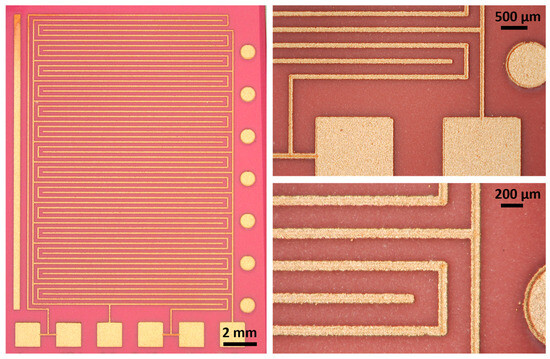
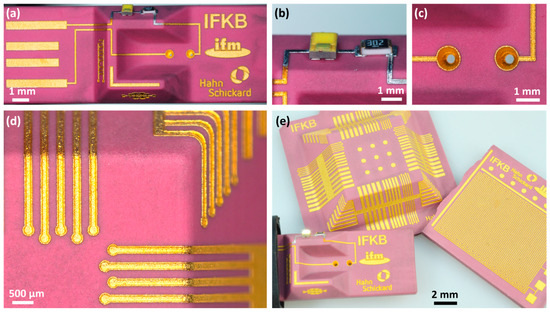
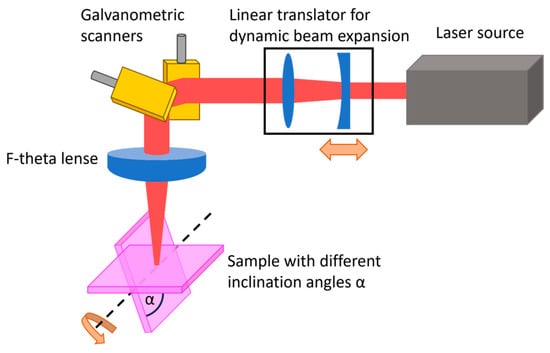
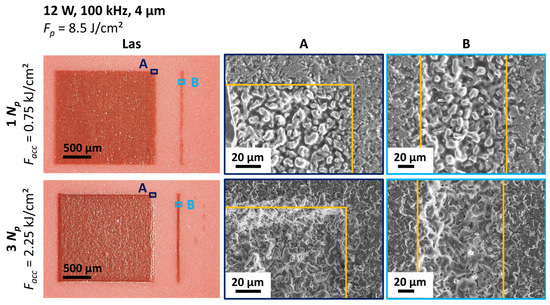
Due to the superior thermal, mechanical and chemical properties of ceramics, metallized ceramics are widely used as circuit carriers and interconnect devices, wherever standard polymer-based circuit boards come to their limits. 2D metallization represents the current state of the art. The metallization of 3D-shaped ceramics cannot be achieved with standard metallization techniques, such as screen printing, but, for example, with the so-called laser-induced direct metallization (LDM). For LDM, a pulsed laser is used to locally activate the ceramic surface, followed by a selective electroless copper plating on the laser-irradiated areas. Although it has already been shown that LDM on Al2O3-based ceramics is possible with different laser systems, a comprehensive study on the effect of different laser parameters on ablation and activation, which includes the influences of structuring on inclined surfaces, has not been done yet. In this study, laser power, pulse repetition frequency, pulse overlap and the number of passes were varied systematically to determine the parametric sensitivity of the ablation and metallization behavior for pulsed infrared laser activation of Cr2O3-doped ZTA. It was found that ablation is necessary for the metallization and that the peak fluence is the governing factor for the ablation and metallization process. It was further shown that ablation can be well predicted with an accumulated fluence, which includes pulse overlap. Structuring under an inclination angle up to 60° does not result in a reduced activation or adhesion strength of the deposited copper. Injection-molded 3D ceramic substrates were successfully metallized and functionalized by applying an optimized set of laser parameters, showing that LDM enables the functionalization of complex 3D ceramic substrates and therefore opens up new possibilities for integrated ceramic circuit carriers.
Full article
Open AccessArticle
Natural Rubber-Based Encapsulation for Wireless Intraruminal Monitoring: Effects of Latex Processing Parameters on Mechanical, Chemical, and RF Transmission Performance
by
Prachid Saramolee, Siraporn Sakphrom, Choosak Rittiphet, Supawat Kotchparadit, Koki Ogura and Sarawuth Chaimool
J. Manuf. Mater. Process. 2026, 10(9), 344; https://doi.org/10.3390/jmmp10090344 - 7 Sep 2026
Abstract
►▼
Show Figures
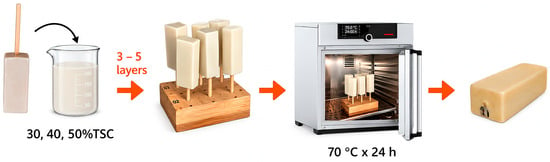
Encapsulation for wireless dairy-cattle implants must resist acidic, moisture-rich gastrointestinal conditions while remaining transparent to radio-frequency (RF) signals. This study evaluated vulcanized natural rubber (NR) latex as an intraruminal encapsulant, examining how total solid content (TSC; 30, 40, 50 wt%), stirring duration (24–72
[...] Read more.
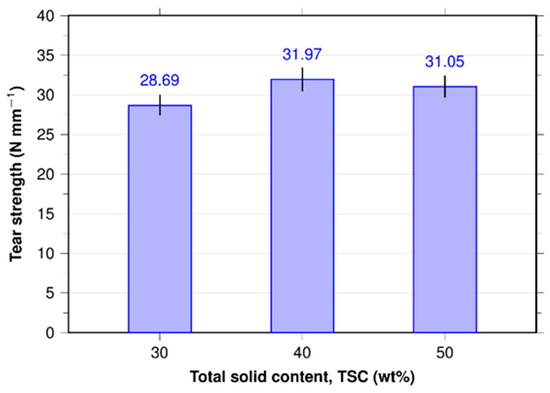
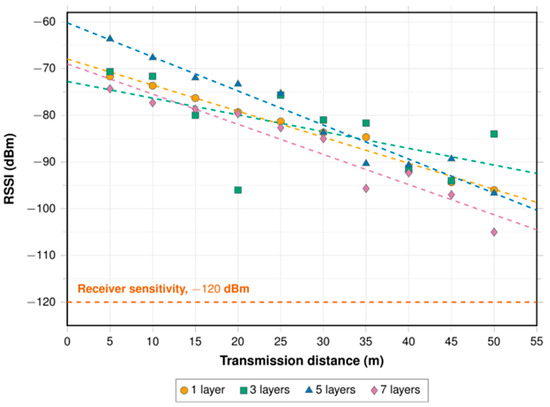
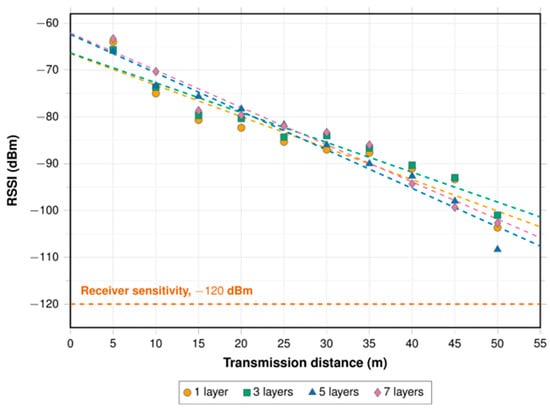
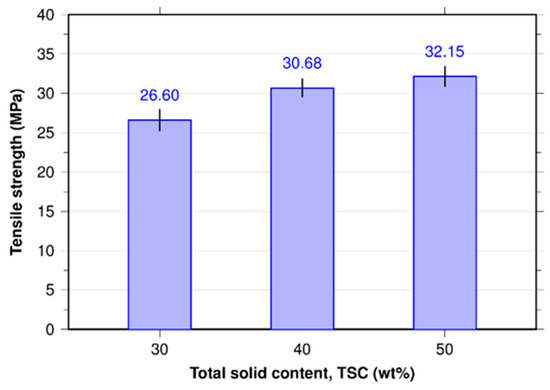
Encapsulation for wireless dairy-cattle implants must resist acidic, moisture-rich gastrointestinal conditions while remaining transparent to radio-frequency (RF) signals. This study evaluated vulcanized natural rubber (NR) latex as an intraruminal encapsulant, examining how total solid content (TSC; 30, 40, 50 wt%), stirring duration (24–72 h), and TiO2 loading affect tensile and tear strength, acidic swelling, dip-coating thickness, and received signal strength indicator (RSSI) at 433 MHz. Multilayer dip-coating produced films 0.25–0.38 mm thick. Tensile strength rose with TSC and stirring (26.6 → 32.2 MPa), whereas tear strength peaked at 40 wt% (31.97 N mm−1). Adding 5 phr (parts per hundred rubber) TiO2 cut pH-4 swelling ~four-fold (21.1 → 5.25%) with a negligible RSSI penalty, and 3–5 coating layers kept the link well above the −120 dBm sensitivity floor over 5–55 m. The optimum—40 wt% TSC, 72 h stirring, 5 phr TiO2—best balanced mechanical integrity, swelling resistance, thickness, and wireless performance. Vulcanized NR is therefore a promising bio-based encapsulant under simulated conditions; dielectric characterization, long-term aging, and in vivo validation remain future work.
Full article

Figure 1
Open AccessArticle
Comparative SPH–Finite Element Assessment of Aerospace Material Systems Under Bird-Strike Loading
by
Mohsen Lalehparvar, Alex Nuttall, Dhruva Bavaria, Felix Massó Etxeberria, Kaustubh Dwivedi, Hessam Ghasemnejad, Pablo Coladas Mato and Wydo van de Waerdt
J. Manuf. Mater. Process. 2026, 10(9), 343; https://doi.org/10.3390/jmmp10090343 - 7 Sep 2026
Abstract
Bird strikes cause aircraft damage, create serious risks to human safety and can contribute to catastrophic incidents, while continuing to impose substantial economic costs on airlines. The impact combines high kinetic energy with discontinuous, strongly nonlinear contact over a short duration, producing large
[...] Read more.
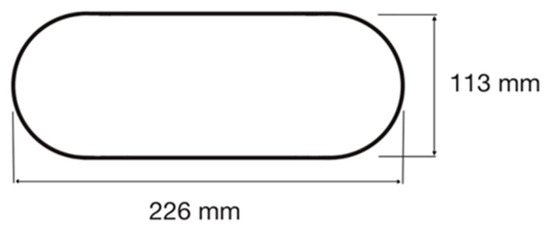
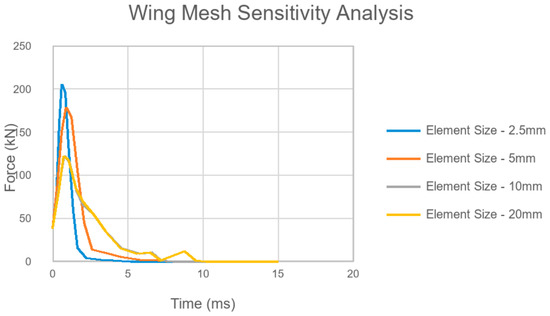
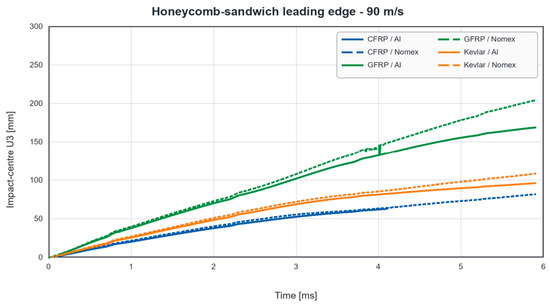
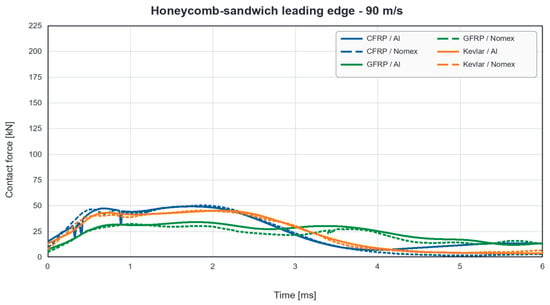
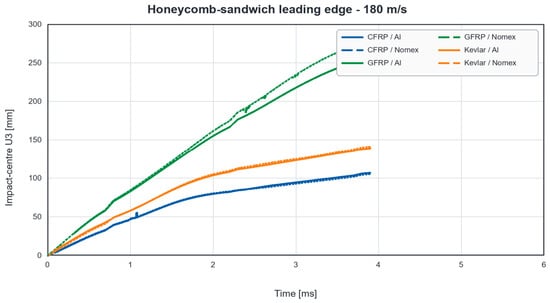
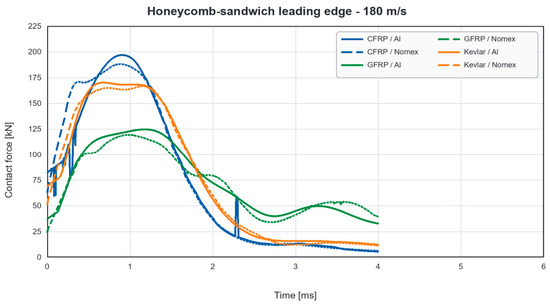
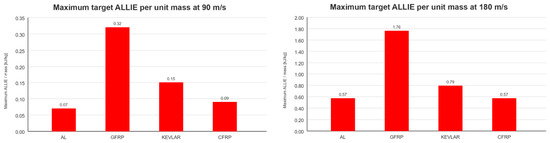
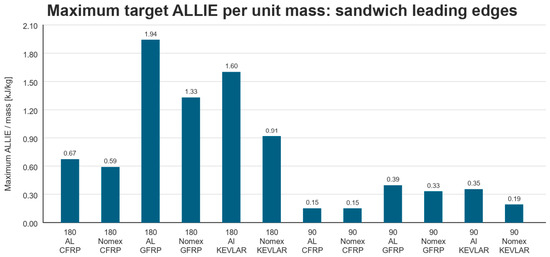
Bird strikes cause aircraft damage, create serious risks to human safety and can contribute to catastrophic incidents, while continuing to impose substantial economic costs on airlines. The impact combines high kinetic energy with discontinuous, strongly nonlinear contact over a short duration, producing large structural deformations; appropriate nonlinear simulation techniques are therefore required to capture this complex interaction. For this purpose, the present study applies established Smoothed Particle Hydrodynamics (SPH)–finite element modelling ingredients to a controlled matrix of aerospace material systems and target geometries. The approach is first benchmarked against a published aluminium flat-plate bird-impact test using a raster-digitised force-history comparison, after which monolithic metallic and composite structures and source-described honeycomb-sandwich alternatives are assessed in flat-panel and curved leading-edge configurations. The results show that contact-force and local-displacement rankings depend strongly on target geometry and response metric, with the curved leading edge changing the ordering observed for the flat panel. More compliant systems generally permit greater local displacement, whereas stiffer systems restrict displacement but can sustain higher short-duration force peaks; consequently, no universal material ranking follows from a single response measure, and the results are most suitable for preliminary design screening.
Full article
(This article belongs to the Special Issue External Field-Assisted Welding and Advanced Processing of Lightweight Metallurgical Structures)
►▼
Show Figures

Figure 1
Open AccessArticle
Water Collection Performance of Additively Manufactured TPMS Condensation Structures in Peltier-Driven Atmospheric Water Generation: Effects of Geometry and Surface Treatment
by
Fatema Tuz Zohra, Hribhu Chowdhury and Bahram Asiabanpour
J. Manuf. Mater. Process. 2026, 10(9), 342; https://doi.org/10.3390/jmmp10090342 - 4 Sep 2026
Abstract
The performance of Peltier-driven atmospheric water generation (AWG) systems depends strongly on the surface geometry and wetting behavior of the condensation structure. Triply periodic minimal surfaces (TPMS) provide high surface area-to-volume ratio and geometric tunability, but their effectiveness as three-dimensional condensation structures requires
[...] Read more.
The performance of Peltier-driven atmospheric water generation (AWG) systems depends strongly on the surface geometry and wetting behavior of the condensation structure. Triply periodic minimal surfaces (TPMS) provide high surface area-to-volume ratio and geometric tunability, but their effectiveness as three-dimensional condensation structures requires experimental evaluation. In this study, five additively manufactured TPMS geometries, Gyroid, Diamond, Lidinoid, SplitP, and Schwarz, were evaluated in a Peltier-driven AWG setup under controlled laboratory conditions. The measured water collection response varied among the tested TPMS geometries, which showed different condensation, retention, and collection trends. Water collection was measured with and without surface treatment, while the monitored surface temperature remained below the calculated dew point during testing. Without surface treatment, total water collection ranged from approximately 0.9 to 1.4 g, whereas surface-treated specimens collected approximately 0.6 to 1.2 g. The specimens with surface treatment exhibited predominantly discrete droplets rather than the film-wise morphology observed without surface treatment, but the total water collection did not increase consistently. Gyroid and Lidinoid showed slight increases with surface treatment, while SplitP, Diamond, and Schwarz showed reductions. Water collection also did not scale directly with calculated TPMS surface area, which suggests that effective air exposure, droplet retention, drainage, and coating uniformity contributed strongly to the observed performance. These findings provide experimental insights into additively manufactured TPMS geometry and surface treatment conditions for Peltier-driven AWG.
Full article
(This article belongs to the Special Issue Application of 3D Printing Technology in Manufacturing and Material Processing)
Open AccessReview
A Review of Meltpool Dynamics and Grain Evolution in Inconel Alloys Produced by Laser Powder Bed Fusion
by
Sanjeevi Sharma R, Venkatachalaiah K N, Ramakrishna Pramod and M. E. Shashi Kumar
J. Manuf. Mater. Process. 2026, 10(9), 341; https://doi.org/10.3390/jmmp10090341 - 3 Sep 2026
Abstract
Laser powder bed fusion (LPBF) is a disruptive additive manufacturing process for producing high-performance Inconel superalloy parts with complex shapes for the aerospace, energy, and other demanding industries. However, uniform part quality remains a persistent challenge, as process parameters, melt-pool dynamics, microstructural evolution,
[...] Read more.
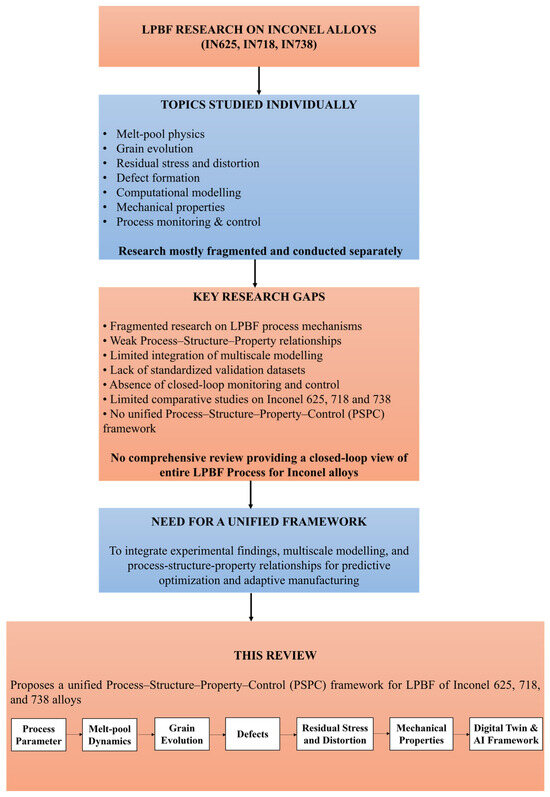
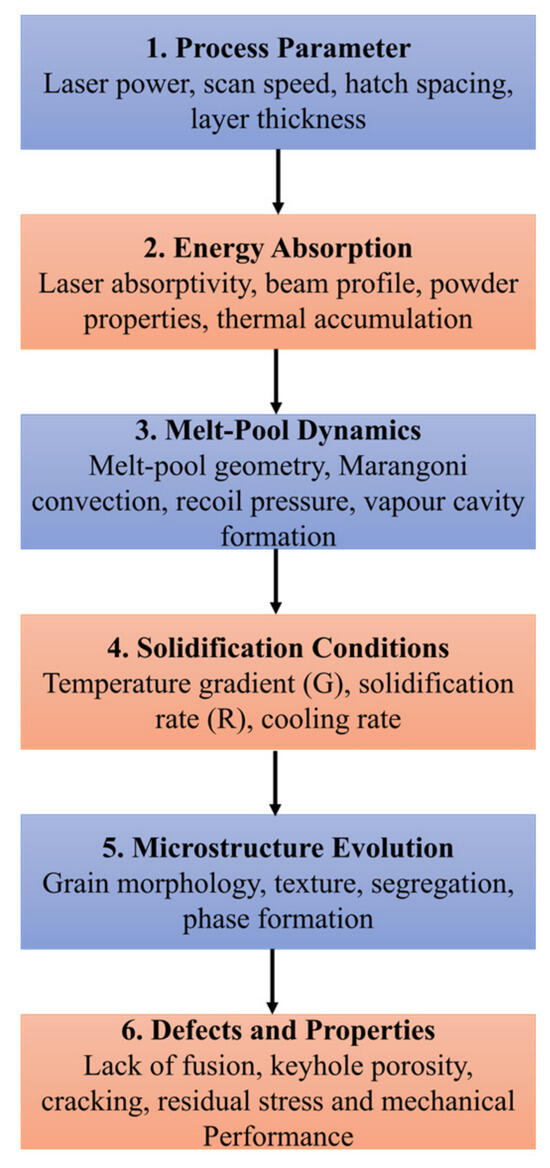
Laser powder bed fusion (LPBF) is a disruptive additive manufacturing process for producing high-performance Inconel superalloy parts with complex shapes for the aerospace, energy, and other demanding industries. However, uniform part quality remains a persistent challenge, as process parameters, melt-pool dynamics, microstructural evolution, defect formation, and mechanical performance are closely coupled across a wide range of spatial and temporal scales. In previous reviews, these dimensions have been considered in isolation with limited insight into their interactions and implications for predictive process control. The present review aims to address this lacuna by proposing a unified Process–Structure–Property–Control (PSPC) framework for LPBF-produced Inconel 625, 718, and 738. The discussion begins with material attributes governing alloy processability, and then synthesises the melt-pool physics governing thermal behaviour, solidification, and energy transfer. Attention then turns to a critical assessment of grain evolution, defect formation, and process stability, showing how the thermal history governs microstructural development and, in turn, mechanical performance via linked process–structure–property relationships. Progress in multiscale numerical modelling, such as finite-element analysis, computational fluid dynamics, phase-field modelling, cellular automata, and phase-diagram calculation (CALPHAD), is reviewed to establish a comprehensive modelling ecosystem for predictive LPBF. The review also discusses the potential of emerging technologies, such as beam shaping, multi-laser processing, in situ monitoring, artificial intelligence, and powder recyclability, to increase the robustness and productivity of the process. Building on these advances, a digital-twin-enabled predictive-manufacturing framework that integrates physics-based models, data-driven algorithms, and real-time monitoring is introduced to enable closed-loop process optimisation. The review ends with a scientific synthesis and future research roadmap for intelligent, reliable, and autonomous LPBF of next-generation Inconel superalloys.
Full article
(This article belongs to the Special Issue Advances in Powder Bed Fusion Technologies)
►▼
Show Figures

Figure 1
Open AccessArticle
Cross-Study of Techniques for the Analysis of Deformations Generated in the Injection Molding Process
by
Vladimir Zagoya-Juárez, Héctor Plascencia-Mora, Jaime Navarrete Damián, Ismael Ruiz-López, Juan Francisco Reveles Arredondo and María Cristina López-Mendez
J. Manuf. Mater. Process. 2026, 10(9), 340; https://doi.org/10.3390/jmmp10090340 - 3 Sep 2026
Abstract
►▼
Show Figures
Injection molding is a plastic material processing technique used in the polymer industry. Because it is a complex process that requires injection cycles to achieve the desired aesthetic quality in the molded parts, it is essential to evaluate and configure all process parameters
[...] Read more.
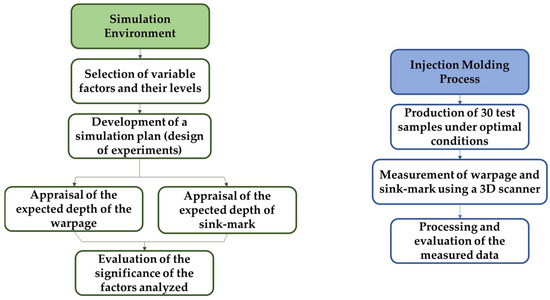
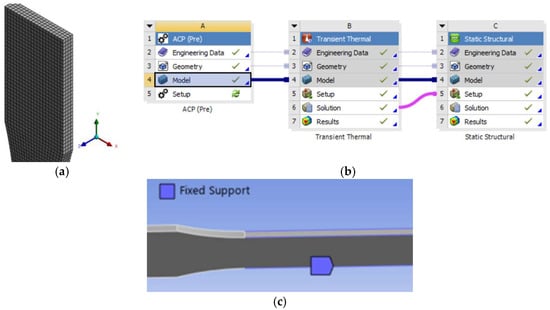
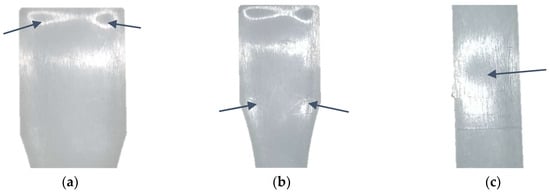
Injection molding is a plastic material processing technique used in the polymer industry. Because it is a complex process that requires injection cycles to achieve the desired aesthetic quality in the molded parts, it is essential to evaluate and configure all process parameters to predict and reduce defects, thereby decreasing the processing time and energy consumption. This study presents the results of tests performed on molded HDPE parts, including modeling and simulation using ANSYS® (2025 R1), a design of experiments (DOE), and 3D scanning of the molded parts. The study compares the behavior of defects (warpages and sink-marks) in molded parts using 3D scanning with the results obtained from coupled thermal-structural field finite element simulations. These simulations were performed using software to assess the residual thermal stress of the ejection phase. The results visually display information that helps designers and engineers in the polymer processing sector evaluate molding-process failures using different software.
Full article

Figure 1
Open AccessArticle
Influence of Process Parameters and Rake Angle on Modeling of Cutting Forces in Wood-Based Materials
by
Oleksandr Burdin, Armin Schleinitz, Florian Morczinek and Martin Dix
J. Manuf. Mater. Process. 2026, 10(9), 339; https://doi.org/10.3390/jmmp10090339 - 2 Sep 2026
Abstract
The environmental impact of technical systems is becoming increasingly important. Particularly in mechanical engineering, with its high demands on process stability and product quality, environmentally beneficial materials such as wood, with its heterogeneous and anisotropic structure, present challenges. Therefore, understanding the cutting process
[...] Read more.
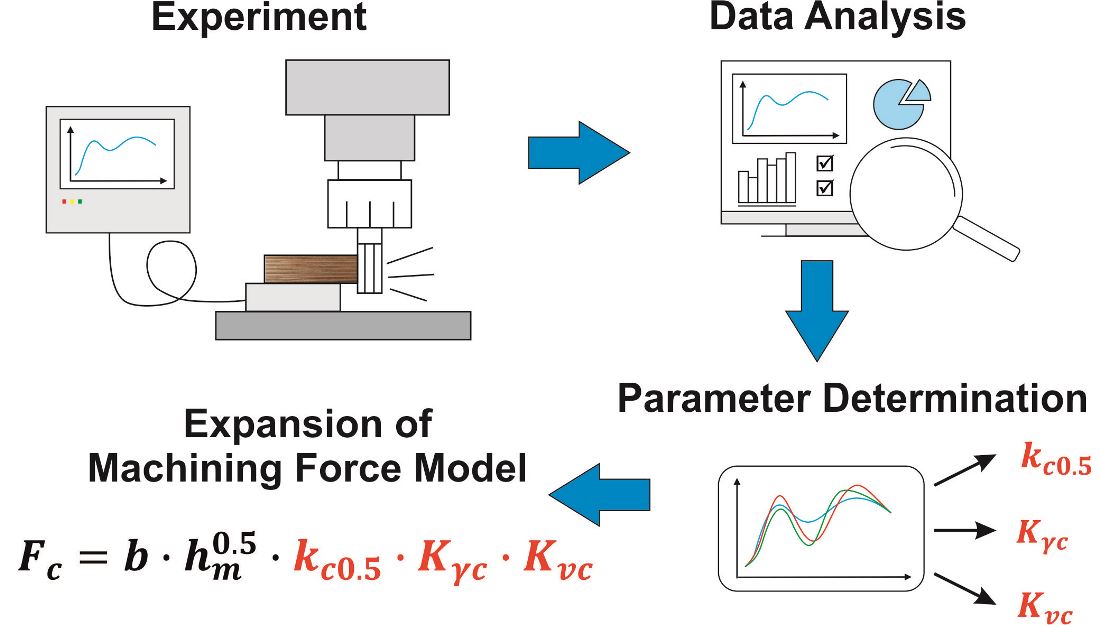
The environmental impact of technical systems is becoming increasingly important. Particularly in mechanical engineering, with its high demands on process stability and product quality, environmentally beneficial materials such as wood, with its heterogeneous and anisotropic structure, present challenges. Therefore, understanding the cutting process and the cutting forces is of great importance. This publication builds upon an established cutting force model and presents experiments to determine the specific cutting force (kc0.5) and normal cutting force (kcN0.5) for birch plywood. Furthermore, the influence of the rake angle (Kγ_c and Kγ_cN) and the cutting speed (Kvc and Kvc) on the cutting forces is investigated. These correction factors are integrated into the established cutting model and verified under the assumption of no relevant directional dependence of the cutting forces due to the fibers of the plywood under investigation at the macroscopic level. The correction factors were determined based on the experiments and show a high degree of agreement with experimentally measured values. The correction factors lead to an increase in accuracy of predicting cutting forces during the peripheral milling of birch plywood. The model enables the prediction of cutting force with an average 30% increase in accuracy compared to the reference model. The results thus allow for a more accurate description of the cutting forces, from which important insights can be derived in the future for optimizing the cutting process and the tool, as well as for addressing tool wear and process quality.
Full article
(This article belongs to the Special Issue Advanced and Sustainable Machining)
►▼
Show Figures

Graphical abstract
Open AccessArticle
Design Optimization of Focus Ring Geometry for Improved Wafer-Edge Ion Energy-Angle Distributions in Pulsed Capacitively Coupled Plasma Etching
by
Sun Jeong Hwang and Hae June Lee
J. Manuf. Mater. Process. 2026, 10(9), 338; https://doi.org/10.3390/jmmp10090338 - 2 Sep 2026
Abstract
Wafer-edge uniformity is a critical issue in plasma etching because local variations in ion bombardment can directly affect the etch profile and process yield. Ion transport near the wafer-edge is strongly influenced by the sheath formed around the boundary between the wafer and
[...] Read more.
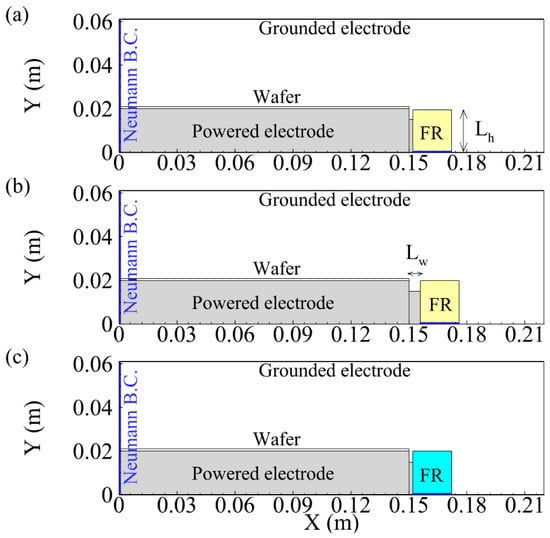
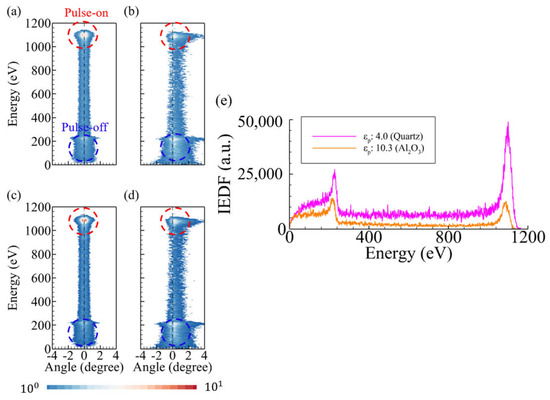
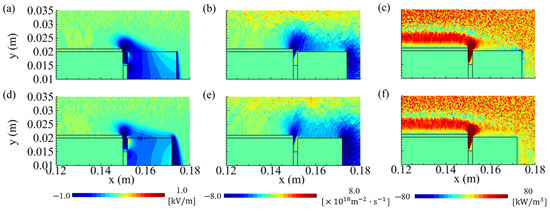
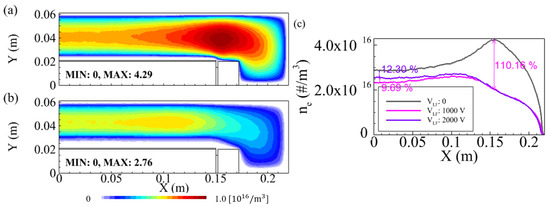
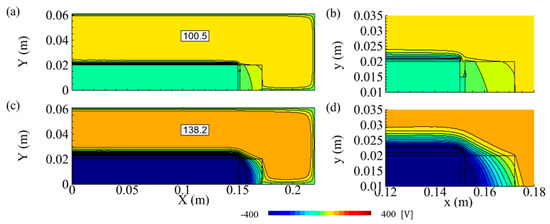
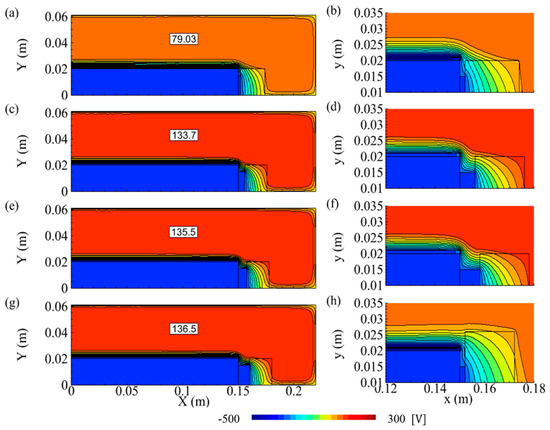
Wafer-edge uniformity is a critical issue in plasma etching because local variations in ion bombardment can directly affect the etch profile and process yield. Ion transport near the wafer-edge is strongly influenced by the sheath formed around the boundary between the wafer and the focus ring. Although focus ring geometry, dielectric properties, and applied voltage conditions can all modify this local sheath, their respective roles in controlling ion incidence angle and energy have not been clearly distinguished. In this study, two-dimensional particle-in-cell Monte Carlo collision simulations were performed for an argon capacitively coupled plasma to compare the effects of focus-ring height, electrode-to-focus-ring gap width, dielectric permittivity, and applied voltage conditions. The electrical conditions included a single-frequency waveform and a pulsed dual-frequency waveform with a variation in the low-frequency (LF) voltage amplitude. Geometric changes in focus-ring height and gap width modify the local sheath contour and ion acceleration direction, leading to more pronounced changes in the ion incidence angle than those caused by dielectric permittivity. The ion energy, however, is more strongly influenced by the applied voltage condition, particularly the LF voltage amplitude. These findings provide fundamental insights into wafer-edge ion control, although their quantitative applicability to reactive and electronegative etching remains to be verified.
Full article
(This article belongs to the Special Issue Recent Developments in Materials Processing for Modern Applications: Advancements and Challenges)
►▼
Show Figures

Figure 1
Open AccessArticle
Functional Architecture and Exploratory Operational Assessment of a Mobile Hydraulic Clay-Brick Molding Machine for Small-Scale Manufacturing
by
Luis Alberto Flores Chaires, José Ricardo Gómez Rodríguez, Hugo Pineda Martínez, Ana Gabriela Castañeda Miranda, Remberto Sandoval Aréchiga, Víktor Ivan Rodríguez Abdala, Salvador Ibarra Delgado and Oscar Osvaldo Ordaz-García
J. Manuf. Mater. Process. 2026, 10(9), 337; https://doi.org/10.3390/jmmp10090337 - 2 Sep 2026
Abstract
►▼
Show Figures
Small-scale clay-brick yards require molding equipment that increases output while remaining mobile, locally serviceable, and compatible with intermittent material supply. This article documents the functional architecture and exploratory operational performance of the mobile 12-cavity hydraulic clay-brick molding machine (ML12). Its design contribution is
[...] Read more.
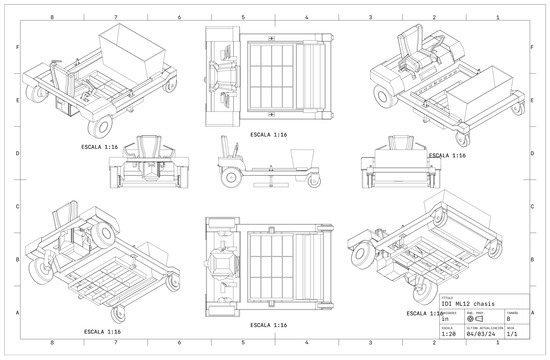
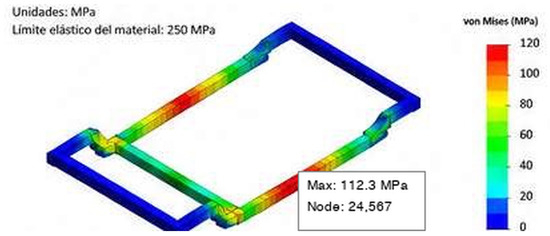
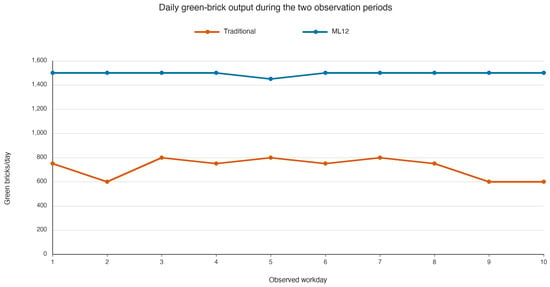
Small-scale clay-brick yards require molding equipment that increases output while remaining mobile, locally serviceable, and compatible with intermittent material supply. This article documents the functional architecture and exploratory operational performance of the mobile 12-cavity hydraulic clay-brick molding machine (ML12). Its design contribution is the integration of a dimensioned wheeled steel chassis, seated paired-lever controls, a translating feed hopper/distributor, a 12-cavity mold, two vertical hydraulic actuators, and a water-spray cleaning subsystem in a four-stage operating cycle. A retrospective concept-appraisal matrix compares this architecture with fixed automated and mobile manual concepts; equal weighting and one-at-a-time ±25% weight variations preserve the ML12’s highest internal score, without establishing stakeholder preference or empirical superiority. The evidence base also comprises sequential daily production logs: ten days of traditional manual molding followed by ten days of ML12-assisted molding. Mean gross green-brick output was 720 ± 86 bricks/day in the traditional period and 1495 ± 16 bricks/day in the ML12 period; corresponding descriptive throughputs were 86.5 and 186.9 bricks/h. A rejection-rate sensitivity analysis shows that, if traditional production had no rejects, ML12 conforming output would equal the traditional gross mean at a 51.8% ML12 rejection rate; this quantity boundary is not an estimate of quality or economic break-even. A preliminary linear-static finite-element case for a reconstructed frame returned a maximum von Mises stress of 112.3 MPa, 1.82 mm resultant displacement, and a minimum elastic safety factor of 2.23 on the reported medium mesh; the result is limited to the specified 1.0 kN load case and is not structural certification of the complete machine. Because the operational comparison was non-randomized and did not control staffing, operators, clay batch, moisture, weather, energy use, or rejection rate, the observed difference cannot be attributed exclusively to the machine. The results establish the machine architecture, an operational signal, and a bounded preliminary frame response, but not brick quality, ergonomic benefit, full structural safety, environmental benefit, or commercial return.
Full article

Figure 1
Open AccessEditorial
Polymer Composites for Additive Manufacturing: Processing, Microstructure, and Mechanical Properties
by
Mohd Shahneel Saharudin
J. Manuf. Mater. Process. 2026, 10(9), 336; https://doi.org/10.3390/jmmp10090336 - 2 Sep 2026
Abstract
Additive manufacturing (AM) has moved beyond prototyping and now produces functional, load-bearing components [...]
Full article
(This article belongs to the Special Issue Innovative and Sustainable Advances in Polymer Composites for Additive Manufacturing: Processing, Microstructure, Machining, and Mechanical Properties)
Open AccessEditorial
Innovative Approaches in Metal Forming and Joining Technologies
by
Mohammad Mehdi Kasaei
J. Manuf. Mater. Process. 2026, 10(9), 335; https://doi.org/10.3390/jmmp10090335 - 2 Sep 2026
Abstract
The continuing evolution of transportation, aerospace, energy, electronics, and other high-performance engineering sectors is placing increasingly demanding requirements on manufacturing technologies [...]
Full article
(This article belongs to the Special Issue Innovative Approaches in Metal Forming and Joining Technologies)
Open AccessArticle
Simulation-Assisted Prediction of Surface Topography for Milling Strategy Selection in Freeform 3-Axis and 5-Axis Ball-End Milling
by
Alejandro Frechilla, Yasser Zekalmi, José Antonio Albajez, María José Oliveros and Sergio Aguado
J. Manuf. Mater. Process. 2026, 10(9), 334; https://doi.org/10.3390/jmmp10090334 - 2 Sep 2026
Abstract
►▼
Show Figures
Surface topography plays a critical role in the functional performance of machined freeform components, yet its assessment traditionally takes place only after manufacturing. This work presents a simulation-assisted framework for predicting the surface topography generated during freeform ball-end milling and using these predictions
[...] Read more.
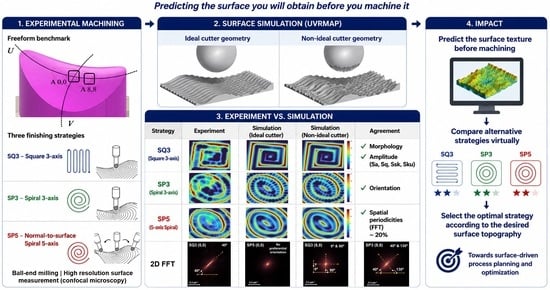
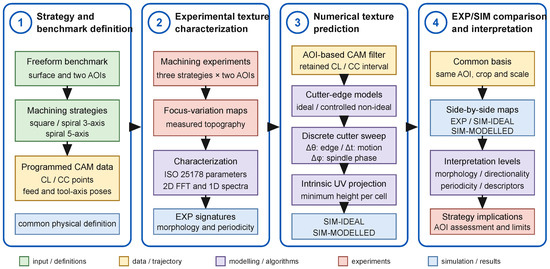
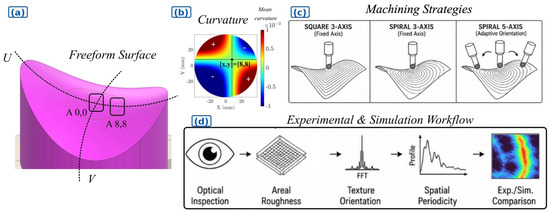
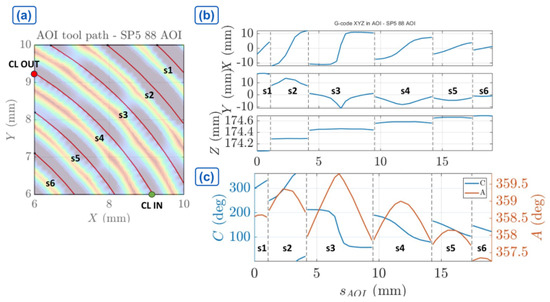
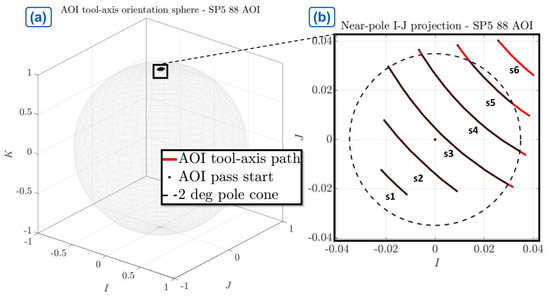
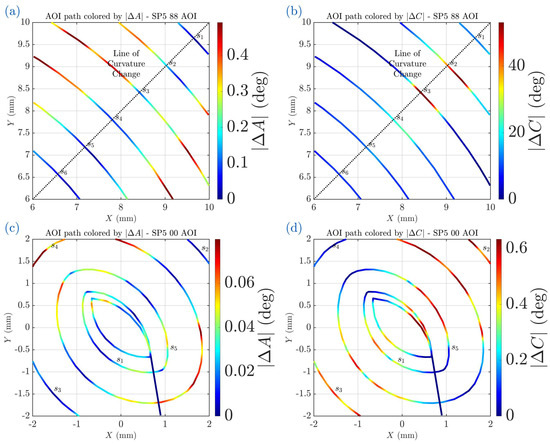
Surface topography plays a critical role in the functional performance of machined freeform components, yet its assessment traditionally takes place only after manufacturing. This work presents a simulation-assisted framework for predicting the surface topography generated during freeform ball-end milling and using these predictions to support machining-strategy selection. Three finishing strategies (3-axis square, SQ3, 3-axis spiral, SP3, and 5-axis spiral, SP5) were investigated on a representative freeform benchmark by combining high-resolution UVRMAP simulations with experimental topography measurements. Surface signatures were characterized using ISO 25178 areal parameters together with two- and one-dimensional Fast Fourier Transform (FFT) analyses, enabling quantitative evaluation of surface amplitude, preferential orientations, anisotropy, and characteristic spatial periodicities. The results demonstrate that machining strategy and local surface geometry produce distinctive topographical signatures that cannot be fully described by conventional roughness parameters alone.Theproposed UVRMAP methodology accurately reproduces the primary spatial organization of the geometric texture generated by the programmed toolpath, while the incorporation of a controlled non-ideal cutter-edge representation improves the prediction of experimentally observed fine-scale features. The combined experimental–simulation methodology provides a robust framework for comparing and validating the spatial and morphological characteristics of predicted surface topographies, providing a basis for future machining-strategy selection according to application-specific surface requirements.
Full article

Graphical abstract
Open AccessArticle
A Study on the Ball Burnishing Main Regime Parameters’ Impact on Manufacturing Lubricating Groove Widths Formed on the Friction Surfaces of Multilayer Connecting Rod Liners
by
Stoyan Slavov, Georgi Valchev, Volodymyr Dzyura, Pavlo Maruschak, Taras Dzhyvak and Islam Zakiev
J. Manuf. Mater. Process. 2026, 10(9), 333; https://doi.org/10.3390/jmmp10090333 - 2 Sep 2026
Abstract
►▼
Show Figures
The present research investigates the optimization of ball burnishing (BB) process parameters to create regular lubricating grooves on multilayer connecting rod liners to prevent engine seizure. The study utilized a Taguchi L9 fractional orthogonal array to evaluate the impact of ball diameter, deforming
[...] Read more.
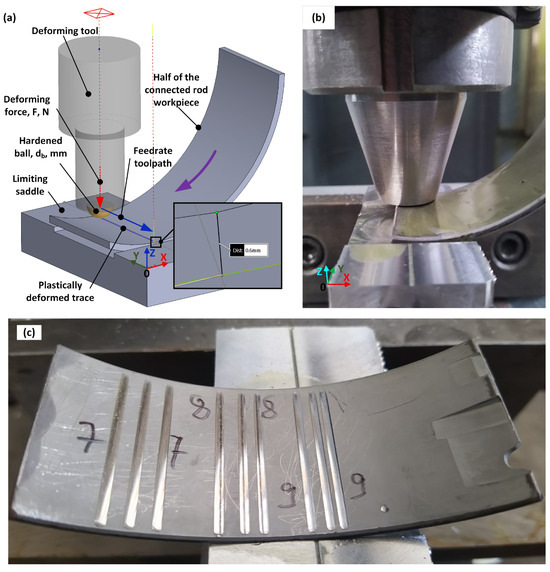
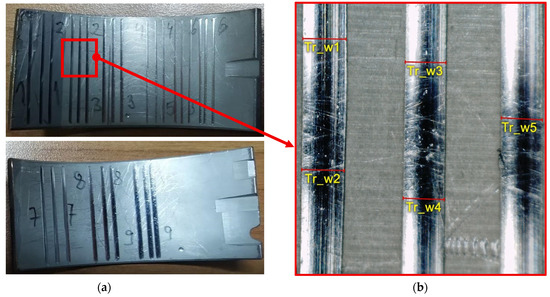
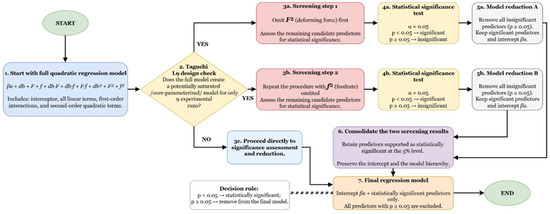
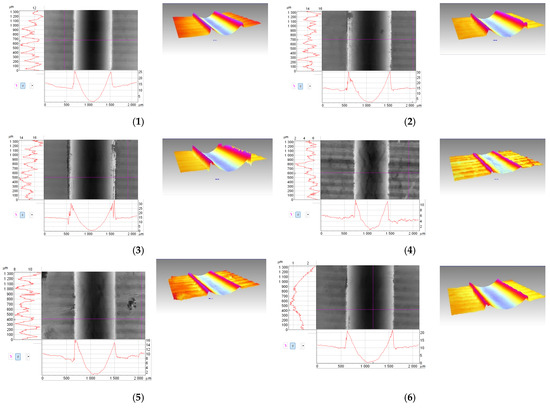
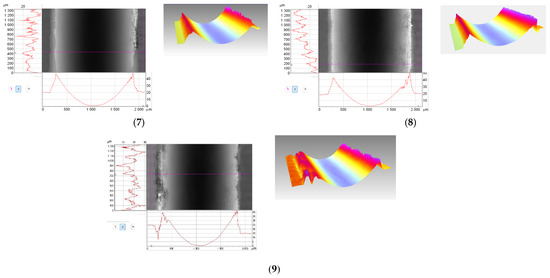
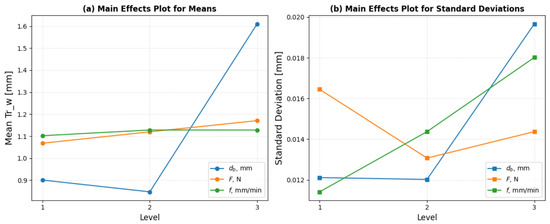
The present research investigates the optimization of ball burnishing (BB) process parameters to create regular lubricating grooves on multilayer connecting rod liners to prevent engine seizure. The study utilized a Taguchi L9 fractional orthogonal array to evaluate the impact of ball diameter, deforming force, and feed rate on the resulting groove widths. Statistical analysis (ANOVA) revealed that ball diameter is the primary driver of groove width variation, exhibiting a non-linear parabolic relationship where the diameter serves as a stabilizing threshold. While deformation force showed a steady linear progression in widening traces, higher feed rates were found to restrict localized plastic flow, resulting in narrower groove widths. For the bimetallic structure (steel back with AlSn20Cu coating), the research recommends tailoring forces to the specific layer—forces for the anti-friction layer and for the substrate to avoid structural destruction. Profilometry confirmed that the height of edge inflows directly correlates with groove depth, ranging from 6 to 30 μm. The optimized non-linear regression model developed in this study achieved an exceptionally high coefficient of determination (R2 = 99.84%), ensuring precise predictive accuracy. Overall, these findings provide a robust framework for researchers to enhance the durability of heavy-duty engine components through controlled surface topography.
Full article

Figure 1
Open AccessArticle
Physics–AI Dual-Driven Prediction of CNC Following-Up Errors and Compensation Control in High Precision Optics Machining
by
Xin Chen, Kai Cheng and Yuanzheng Fu
J. Manuf. Mater. Process. 2026, 10(9), 332; https://doi.org/10.3390/jmmp10090332 - 2 Sep 2026
Abstract
Optical surface deviations in ophthalmic optics arise from fast tool servo errors, the tool footprint, freeform surface residuals, and the freeform surface curvature responses across processing stages. In this paper, a PAM-Net physics–AI dual-driven compensation control method is presented for addressing the issues
[...] Read more.
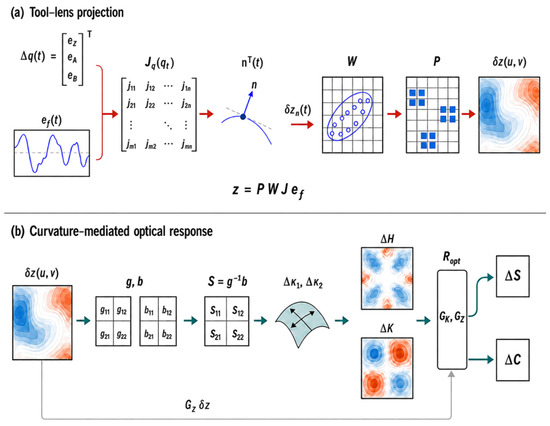
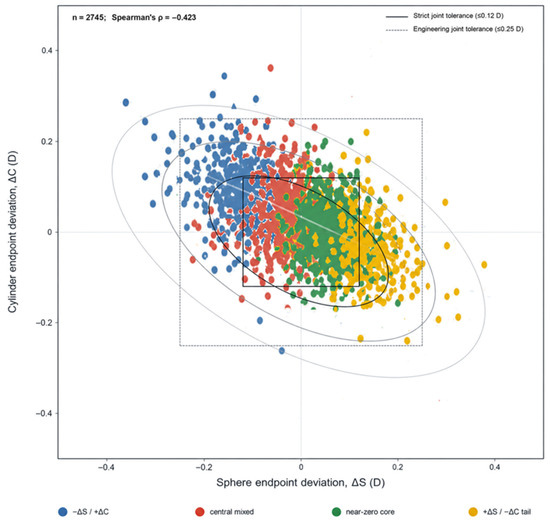
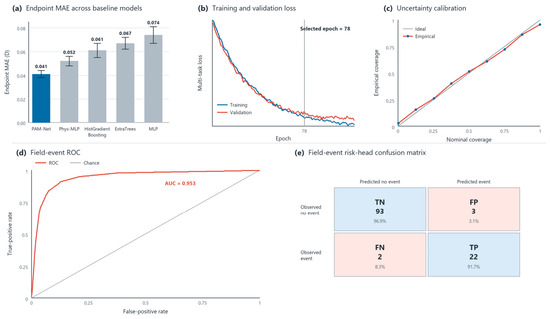
Optical surface deviations in ophthalmic optics arise from fast tool servo errors, the tool footprint, freeform surface residuals, and the freeform surface curvature responses across processing stages. In this paper, a PAM-Net physics–AI dual-driven compensation control method is presented for addressing the issues in dynamically accurate positioning of a diamond cutting tool via the fast tool servo using existing methods, e.g., struggling to characterize micrometer-scale CNC following-up errors, spatial surface-form perturbations, and S/C optical quality simultaneously. PAM-Net maps Z-axis position, velocity, acceleration, jerk, and A/B-axis phases to surface-form residuals and S/C deviations through tool-lens projection and curvature-mediated optical-response operators, while jointly estimating uncertainty and safety risk for constrained NC compensation. The framework also preserves an interpretable mediation chain from servo dynamics to final optical quality. On holdout-35, removing acceleration/jerk increased RMSE from 0.512 to 5.395 μm, indicating strong predictive dependence on high-order servo dynamics. Closed-loop validation increased the strict ±0.12 D pass rate from 72.5% to 87.5%, alongside reduced surface-form and curvature residuals. These results indicate that learning-based compensation control for high-precision freeform-optics manufacturing requires joint consideration of prediction accuracy, physical interpretability, executable NC write-back, and manufacturing constraints.
Full article
(This article belongs to the Special Issue Next-Generation Machine Tools and Machining Technology)
►▼
Show Figures

Figure 1
Open AccessArticle
Influence of Processing Parameters on Microstructure, Crystallographic Texture, and Tensile Behavior in Dissimilar Friction Stir-Welded Ti–6242 SG and Ti–54M
by
Kapil Gangwar and Mamidala Ramulu
J. Manuf. Mater. Process. 2026, 10(9), 331; https://doi.org/10.3390/jmmp10090331 - 1 Sep 2026
Abstract
Dissimilar friction stir welding (FSW) of titanium alloys offers a route to spatially optimized aerospace structures, but the asymmetric thermomechanical environment produces heterogeneous microstructures and textures whose interaction with mechanical performance is not well characterized. A near-α/α+β combination of titanium alloys, Ti–6242 SG
[...] Read more.
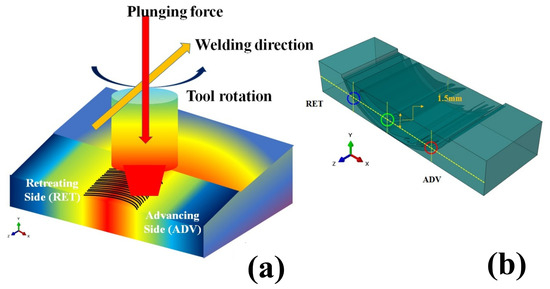
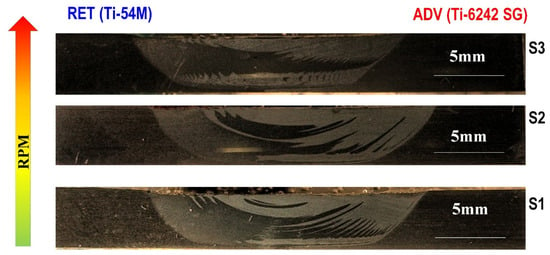
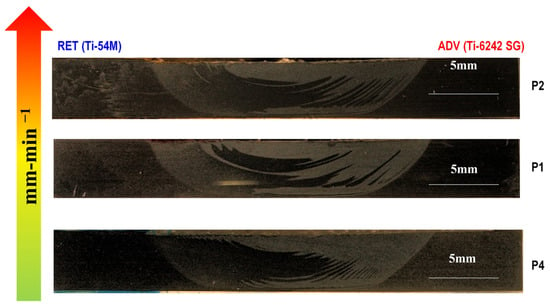
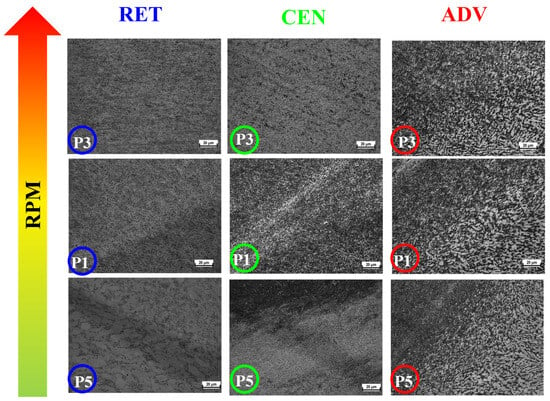
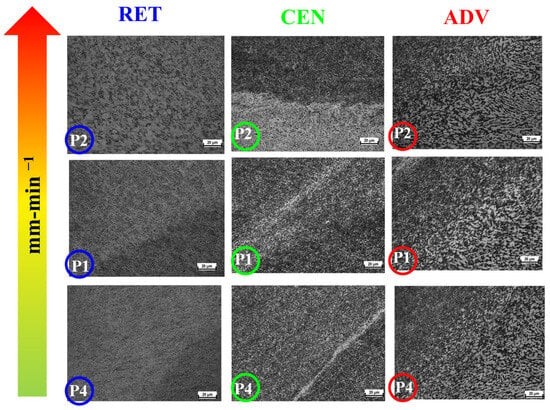
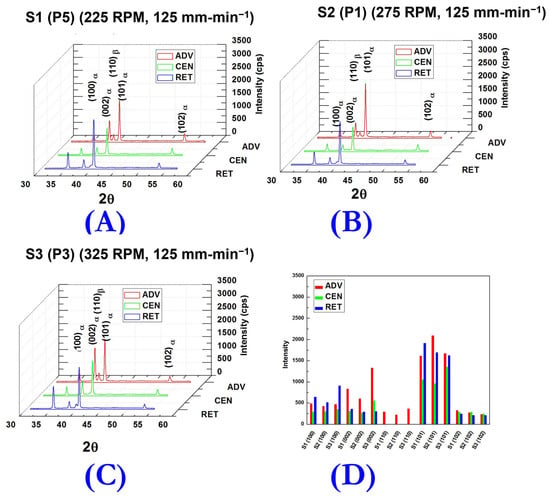
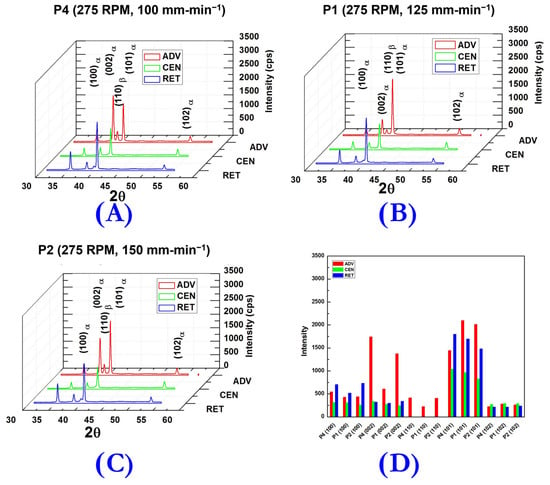
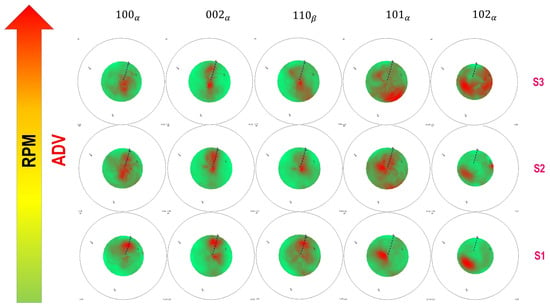
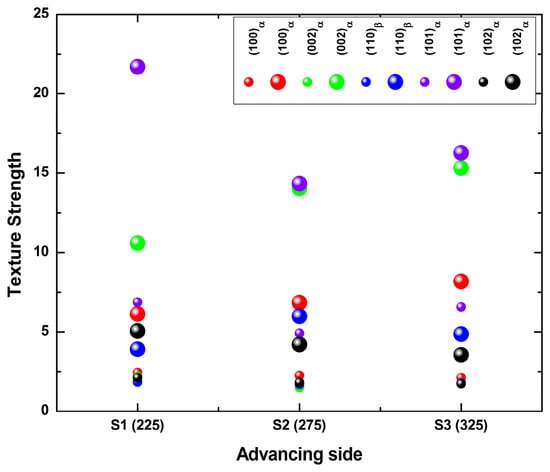
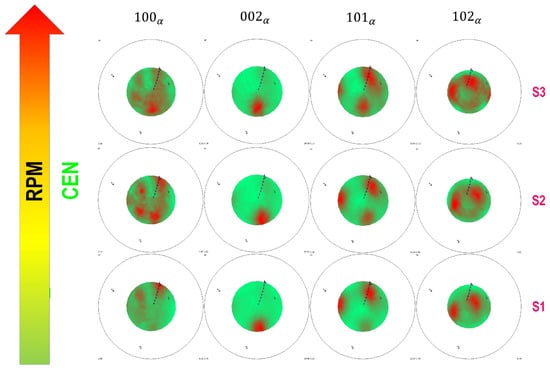
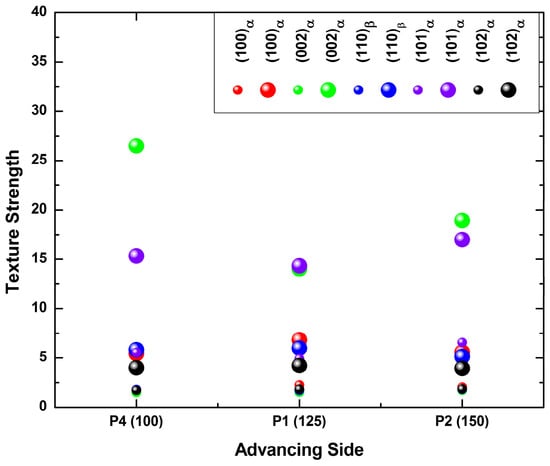
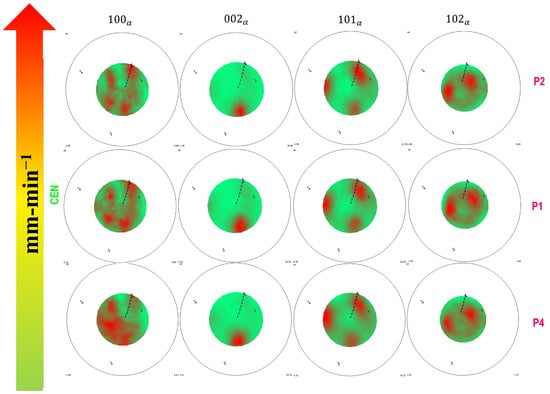
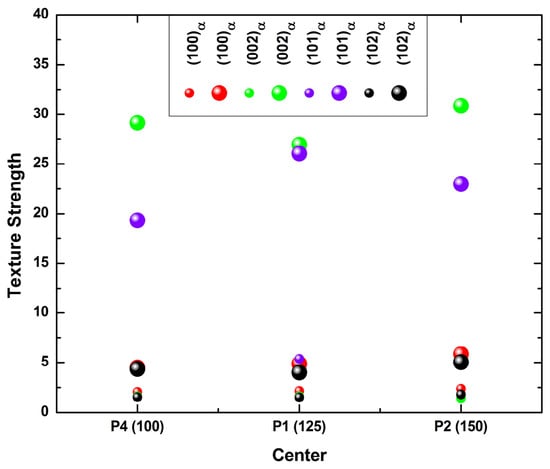
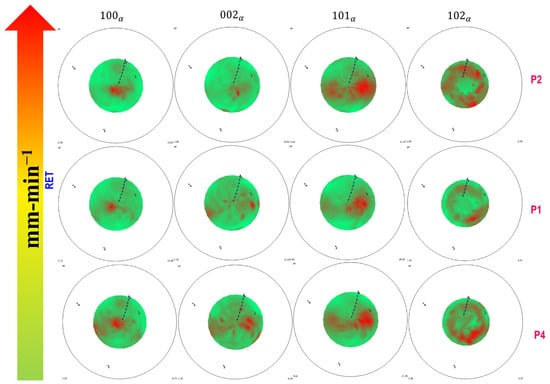
Dissimilar friction stir welding (FSW) of titanium alloys offers a route to spatially optimized aerospace structures, but the asymmetric thermomechanical environment produces heterogeneous microstructures and textures whose interaction with mechanical performance is not well characterized. A near-α/α+β combination of titanium alloys, Ti–6242 SG (advancing side, ADV) and Ti–54M (retreating side, RET), was welded across a matrix of rotation speeds (225–325 rpm) and traverse speeds (100–150 mm·min−1), spanning rotation-to-traverse-speed ratios N/v of 1.80–2.75, which was used throughout as an empirical processing index that orders the conditions of this matrix rather than as a measure of specific heat input. Microstructure, phase identification, relative diffracted-intensity trends, and crystallographic textures were characterized by 2D-XRD at three cross-section locations (ADV, weld nugget center [CEN], RET) and correlated with transverse tensile properties and fracture locations. Partial pole figures were plotted in the simple-shear reference frame with ideal-orientation overlays, intensities in multiples of a random distribution (m.r.d.). The CEN develops the strongest textures, dominated by a basal {002}α component (20–31 m.r.d.) with poles near the normal direction; this concentration lies away from the ideal shear fiber loci and is more readily explained by orientation inheritance during the β→α transformation on cooling than by direct shear, although unambiguous identification of variant selection would require orientation-resolved measurements. The RET develops {101}α and {100}α pole concentrations clustering near the ideal P-fiber loci, consistent with deformation-related texture development, intensifying with both rotation and traverse speed. The ADV shows mixed textures varying non-monotonically with parameters. Two conditions of nearly identical N/v obtained from different parameter combinations (225 rpm/125 mm·min−1 and 275 rpm/150 mm·min−1) nevertheless develop measurably different streak morphologies, microstructures, textures, and tensile responses, showing directly that N/v orders but does not determine the thermomechanical state. Yield strength is uniform (≈900–940 MPa) across the full matrix, consistent with a Schmid-factor estimate in which the basal-near-ND CEN texture gives a very low resolved shear stress on basal systems under transverse loading; joint efficiencies reach ≈90–96%. Ductility, in contrast, tracks consolidation quality rather than texture severity: fracture strain rises almost monotonically with N/v, from ≈0.6–1.4% at N/v ≈ 1.8 (defect-driven, erratic failure) to ≈5.4–6.0% at N/v = 2.60, despite the latter condition carrying the strongest RET pyramidal texture. Full-field strain measurement shows the weld nugget to carry the lowest strain and the highest apparent stiffness of any zone in every condition for which the load record is reliable, with strain accumulating on the advancing side. Consolidated conditions fracture on the advancing side where deformation concentrates, whereas the lowest N/v and longest-exposure conditions fracture in the nugget center; all fracture surfaces are ductile, with the crack path following continuous α layers at prior-β grain boundaries. A favorable processing range within the investigated parameter matrix is N/v ≈ 2.2–2.6, with the best overall combination at 325 rpm and 125 mm·min−1 (N/v = 2.60: UTS ≈ 1010 MPa, ≈5.4–6.0% elongation). Within the parameter range examined here, consolidation quality is the first-order design variable for this dissimilar system, with the zonal texture architecture setting the yield strength level.
Full article
(This article belongs to the Special Issue Recent Advances in Welding and Joining Metallic Materials)
►▼
Show Figures

Figure 1
Open AccessArticle
A Parameter-Less Multi-Objective Optimization Framework for Additive, Thermal, and Subtractive Manufacturing Processes
by
Ravipudi Venkata Rao, Ajinkya Kishor Salve and Joao Paulo Davim
J. Manuf. Mater. Process. 2026, 10(9), 330; https://doi.org/10.3390/jmmp10090330 - 1 Sep 2026
Abstract
Multi-objective optimization has become an indispensable tool for solving engineering design and manufacturing problems involving multiple conflicting objectives. This paper presents a novel parameter-less multi-objective optimization (MOO) framework that combines the strengths of evolutionary MOO techniques with the parameter-free search philosophy of the
[...] Read more.
Multi-objective optimization has become an indispensable tool for solving engineering design and manufacturing problems involving multiple conflicting objectives. This paper presents a novel parameter-less multi-objective optimization (MOO) framework that combines the strengths of evolutionary MOO techniques with the parameter-free search philosophy of the Jaya and Rao algorithms. The proposed framework incorporates non-dominated sorting, elite archiving, and crowding-distance mechanisms to achieve an effective balance between convergence and diversity while eliminating the need for algorithm-specific control parameters. The proposed framework is first validated on sixteen widely used unconstrained benchmark problems comprising five ZDT, seven DTLZ, two IDTLZ, and two SDTLZ test suites using the maximum number of function evaluations reported in the literature. Its performance is evaluated using five widely accepted quality indicators, namely Generational Distance (GD), Inverted Generational Distance (IGD), Hypervolume (HV), Spacing (SP), and Spread (SD). The benchmark results demonstrate that the proposed framework produces competitive Pareto-optimal fronts and exhibits excellent convergence, diversity, and solution distribution compared with several state-of-the-art evolutionary multi-objective optimization algorithms. The practical applicability of the proposed framework is demonstrated through five representative manufacturing optimization problems involving Selective Laser Melting, Microwave Hybrid Heating, Sustainable Machining, Wire Electrical Discharge Machining, and Wire Arc Additive Manufacturing. These case studies encompass additive, thermal, subtractive, and many-objective manufacturing optimization problems with conflicting performance measures. The generated Pareto-optimal solutions are subsequently ranked using the recently developed BHARAT (Best Holistic Adaptable Ranking of Attributes Technique) multi-attribute decision-making method to identify the most suitable compromise solutions. The obtained results demonstrate that the proposed parameter-less MOO framework provides a simple approach with competitive convergence, diversity, and decision-support capabilities for complex manufacturing optimization problems.
Full article
Open AccessArticle
Active Vibration-Based Structural Health Monitoring of CFRP Beams and Plates Using an Elastoplastic Hysteresis Model of the Nonlinear Resonant Response
by
Oleh Derkach, Andrejs Kovalovs, Valerii Kobzar and Artem Ratynskyi
J. Manuf. Mater. Process. 2026, 10(9), 329; https://doi.org/10.3390/jmmp10090329 - 1 Sep 2026
Abstract
An active vibration-based methodology for structural health monitoring of polymer-matrix composites is presented, in which piezoelectric actuators excite resonant vibrations and the diagnostic information is carried by two nonlinear characteristics: the backbone curve and the amplitude-dependent logarithmic decrement. Both are described by a
[...] Read more.
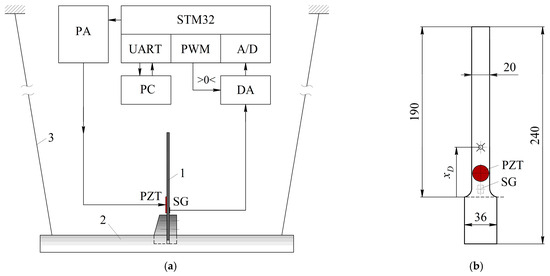
An active vibration-based methodology for structural health monitoring of polymer-matrix composites is presented, in which piezoelectric actuators excite resonant vibrations and the diagnostic information is carried by two nonlinear characteristics: the backbone curve and the amplitude-dependent logarithmic decrement. Both are described by a single elastoplastic model of the Iwan (microplasticity) type with a power-law distribution of yield thresholds. The two characteristics share a common power-law exponent, and the model predicts a parameter-free ratio between the modulus defect and the hysteretic intensity. The four parameters are identified by a joint Bayesian fit. The methodology is applied to two carbon-fiber-reinforced polymer objects: a cantilever beam with a symmetric stacking sequence (three modes, 87 to 1431 Hz) and a plate strip with an unsymmetric one (two modes near 34 and 203 Hz), each tested intact and after controlled local damage. The measured ratio reproduces the prediction within 4 to 12%; whereas, the fundamental plate mode reveals a non-frictional, matrix-dominated dissipation. Local damage increases the hysteretic intensity 1.4 to 2.3 times and the modulus defect up to 2.7 times, while the resonant frequency changes by less than 0.8% and the background decrement remains nearly unchanged, giving a compact damage signature with minimal baseline requirements.
Full article
(This article belongs to the Special Issue Processing, Mechanical Properties, and Manufacturing Techniques of Advanced Composite Materials)
►▼
Show Figures

Figure 1
Open AccessArticle
Layer-Wise Geometric Deviation Prediction in Metal Additive Manufacturing Using a Geometrically Informed cGAN and X-Ray Computed Tomography
by
Himal Sapkota, Prateek Neupane, Ehsan Mehrdad, Hongbing Lu and Sangjin Jung
J. Manuf. Mater. Process. 2026, 10(9), 328; https://doi.org/10.3390/jmmp10090328 - 1 Sep 2026
Abstract
Geometric deviations in unsupported overhang features pose one of the most persistent quality challenges in Laser Powder Bed Fusion (LPBF), where even small deviations from the intended geometry can undermine part functionality and reliability. This study presents a geometrically informed conditional Generative Adversarial
[...] Read more.
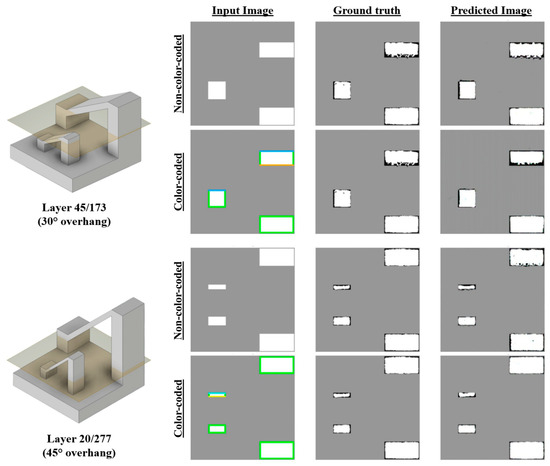
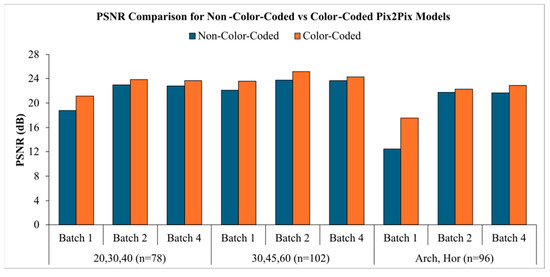
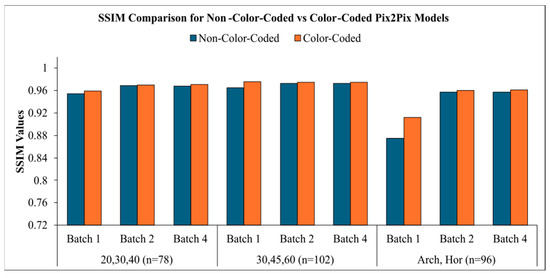
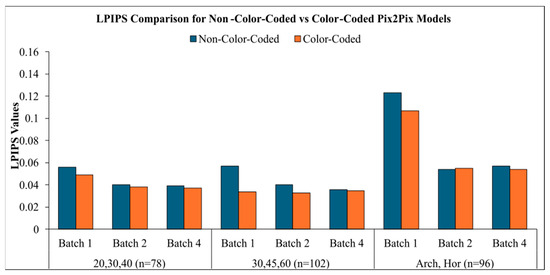
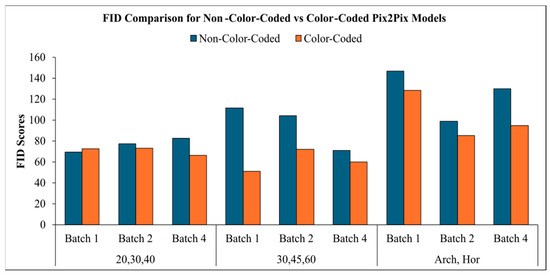
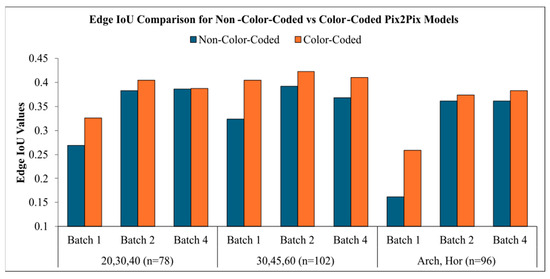
Geometric deviations in unsupported overhang features pose one of the most persistent quality challenges in Laser Powder Bed Fusion (LPBF), where even small deviations from the intended geometry can undermine part functionality and reliability. This study presents a geometrically informed conditional Generative Adversarial Network (cGAN), implemented through the Pix2Pix framework, to predict layer-wise geometric deviations in LPBF-printed parts with overhang geometries, using paired two-dimensional Computer-Aided Design (2D CAD) slices and corresponding X-ray Computed Tomography (XCT)-derived ground truth slices. The study investigates how geometric information can be encoded within the conditional input of the Pix2Pix framework to more effectively guide deviation prediction. A total of 18 models were trained and evaluated across multiple overhang geometry groups and batch size configurations, assessed through a combination of perceptual, structural, and boundary-focused metrics, namely Peak Signal-to-Noise Ratio (PSNR), Structural Similarity Index Measure (SSIM), Learned Perceptual Image Patch Similarity (LPIPS), Fréchet Inception Distance (FID), and Edge Intersection over Union (Edge IoU). The results demonstrated that color-coded inputs consistently improved prediction fidelity, perceptual similarity, and edge alignment relative to their non-color-coded counterparts. Furthermore, a model trained on a balanced multi-geometry dataset showed improved prediction performance on withheld 30° and 60° overhang configurations within the benchmark geometry family. The proposed framework offers a data-driven, design-stage tool for anticipating geometry-dependent deviations in LPBF overhang structures, supporting design for additive manufacturing.
Full article
(This article belongs to the Special Issue Smart Manufacturing in the Era of Industry 4.0, 2nd Edition)
►▼
Show Figures

Figure 1
Open AccessArticle
Mechanism-Driven Design and Validation of a Multi-Material Polymeric Auxetic for Deformation-Activated Sealing
by
Henry Titchener-Hooker, Rakan Albarakati, Hany Hassanin and Khamis Essa
J. Manuf. Mater. Process. 2026, 10(9), 327; https://doi.org/10.3390/jmmp10090327 - 1 Sep 2026
Abstract
►▼
Show Figures
Auxetic polymers offer a route to deformation-activated sealing by transforming axial deformation into lateral expansion, enabling controlled conformity and retention within perforated structures. This paper presents the design-space-guided optimisation of a multi-material polymeric auxetic plug for mechanically activated sealing of circular perforation surrogates
[...] Read more.
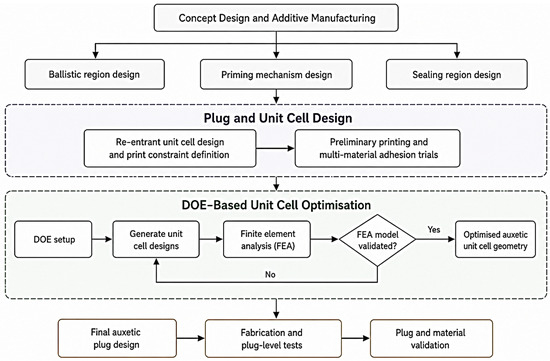
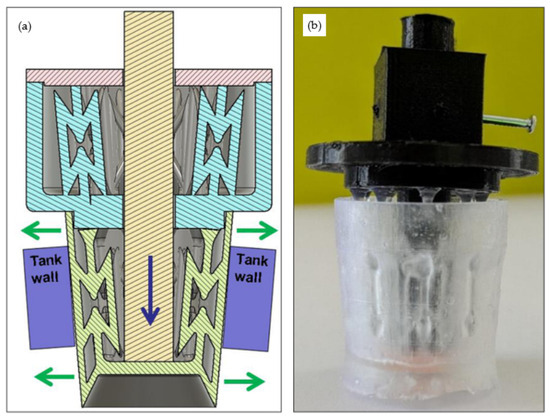
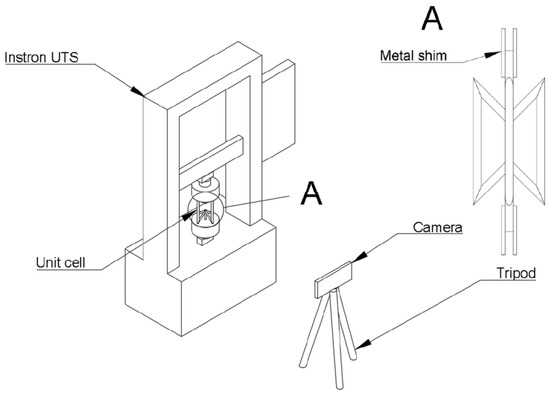
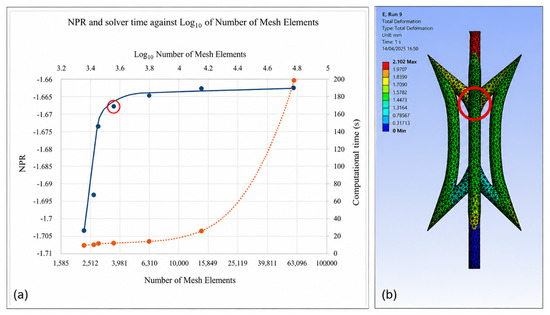
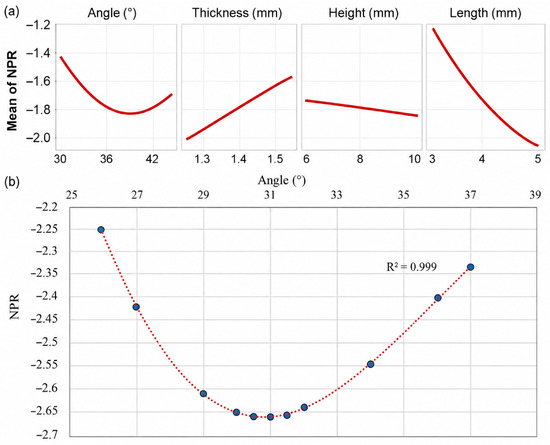
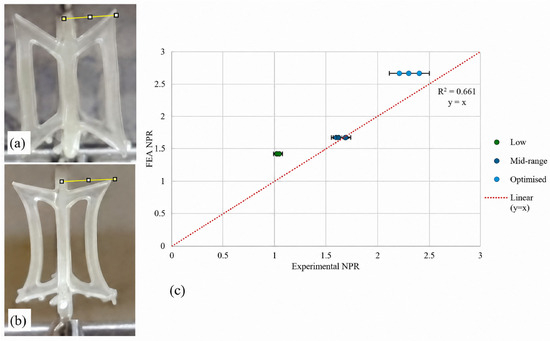
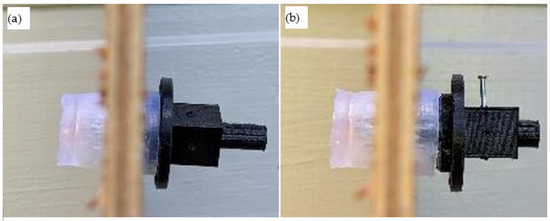
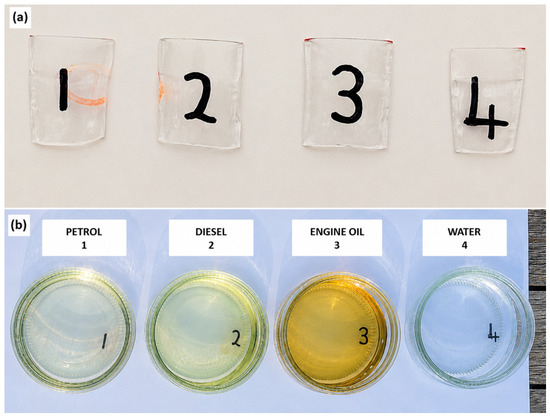
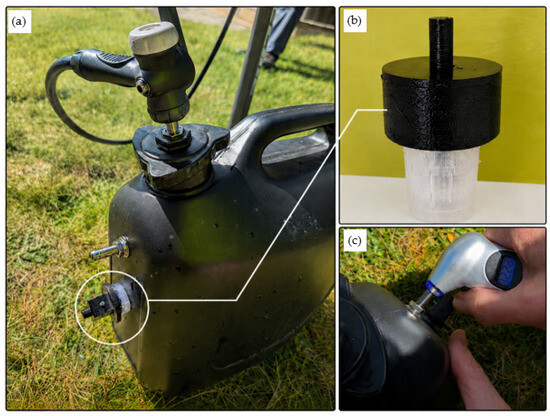
Auxetic polymers offer a route to deformation-activated sealing by transforming axial deformation into lateral expansion, enabling controlled conformity and retention within perforated structures. This paper presents the design-space-guided optimisation of a multi-material polymeric auxetic plug for mechanically activated sealing of circular perforation surrogates relevant to military ground-vehicle structures using a controlled thin-wall surrogate validation framework. The sealing combines an SLA-printed Elastic 50A photopolymer auxetic body with TPU 95A load-transfer and priming components. A parameterised re-entrant unit cell was optimised using response-surface design of experiments coupled with nonlinear finite-element analysis. The optimised geometry, with a height of 6 mm, length of 5 mm, strut thickness of 1.25 mm, and re-entrant angle of 31°, achieved a predicted negative Poisson’s ratio of −2.66 under 20% axial strain. Experimental validation using additively manufactured unit cells confirmed the intended auxetic deformation response. The optimised structure was then integrated into a multi-material plug and tested against a solid polymer benchmark, achieving sealing to approximately 22 kPa with improved anchoring across the tested 22–25 mm perforation range. The results establish a mechanism-driven pathway from polymer auxetic unit-cell optimisation to plug-level pressure-sealing performance, demonstrating the potential of multi-material auxetic architectures as deformation-activated sealing systems for temporary repair of perforated military ground-vehicle structures.
Full article

Figure 1
Open AccessArticle
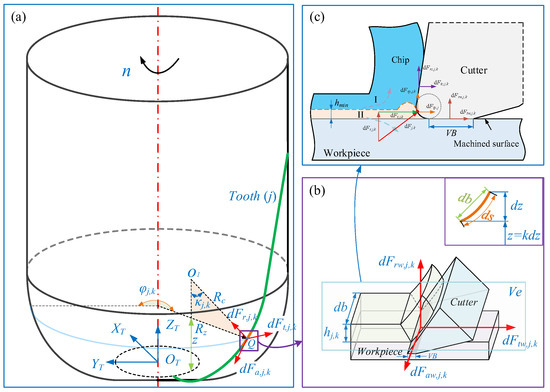
Accurate Prediction of Cutting Force and Force-Induced Deformation in End Milling of Titanium Alloy Thin-Walled Parts Considering Tool Wear and Material Removal
by
Yanjie Du, Chuanqi Zhu, Chenghui Wu and Yuwen Sun
J. Manuf. Mater. Process. 2026, 10(9), 326; https://doi.org/10.3390/jmmp10090326 - 1 Sep 2026
Abstract
Titanium alloy thin-walled parts are widely used in the aerospace industry because of their excellent high-temperature performance. However, their low structural stiffness and poor machinability often result in substantial machining deformation and severe tool wear, thereby reducing machining accuracy and surface quality. To
[...] Read more.
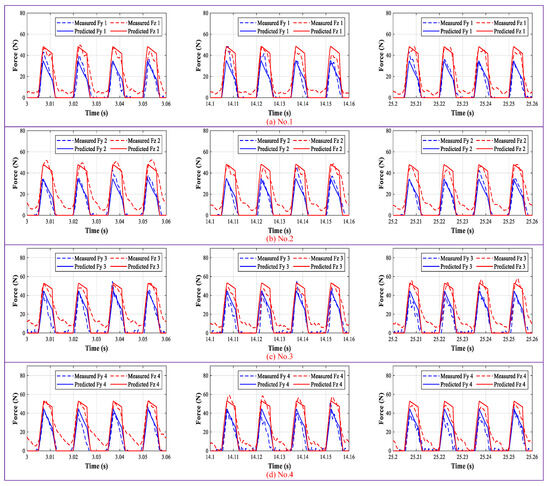
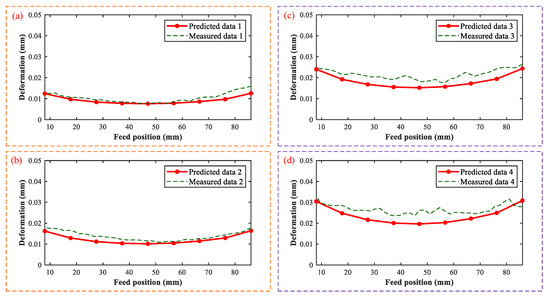
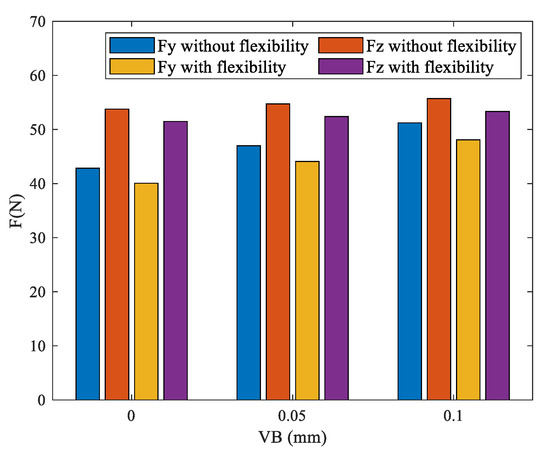
Titanium alloy thin-walled parts are widely used in the aerospace industry because of their excellent high-temperature performance. However, their low structural stiffness and poor machinability often result in substantial machining deformation and severe tool wear, thereby reducing machining accuracy and surface quality. To address these issues, an accurate method is proposed for predicting cutting force and force-induced deformation in the end milling of titanium alloy thin-walled parts while considering tool wear and material removal. First, a cutting force model incorporating tool wear is established to characterize the influence of tool wear on milling forces during titanium alloy machining. Subsequently, a force-induced deformation model is developed based on small-deflection theory to describe the deformation response of the flexible workpiece under milling loads. Furthermore, an iterative strategy is proposed to predict the coupled evolution of cutting force and force-induced deformation during successive material removal. In this strategy, the element stiffness matrix is updated at different feed positions according to the evolving material removal state, while the effects of workpiece deformation on the actual cutting state are incorporated into the cutting force calculation. This provides a framework for accurately predicting cutting force and force-induced deformation. Multilayer end-milling experiments were conducted for validation. The average peak-value errors of Fy and Fz were 7.8% and 5.5% for the new tool and 5.9% and 6.1% for the tool with VB = 0.05 mm, respectively, while the corresponding average deformation prediction errors were 11.8% and 14.5%. These results demonstrate the accuracy of the proposed method.
Full article
(This article belongs to the Special Issue Prediction and Estimation of Tool Wear and Failure in the Milling Process of Difficult-to-Cut Materials)
►▼
Show Figures

Figure 1
Journal Menu
► ▼ Journal Menu-
- JMMP Home
- Aims & Scope
- Editorial Board
- Reviewer Board
- Topical Advisory Panel
- Early Career Editorial Board
- Instructions for Authors
- Special Issues
- Topics
- Article Processing Charge
- Indexing & Archiving
- Editor’s Choice Articles
- Most Cited & Viewed
- Journal Statistics
- Journal History
- Journal Awards
- Conferences
- Editorial Office
Journal Browser
► ▼ Journal BrowserHighly Accessed Articles
Latest Books
E-Mail Alert
News
Topics
Topic in
Coatings, Lubricants, Metals, Applied Sciences, CMD, JMMP
Surface Modification and Durability Enhancement of Advanced Alloys
Topic Editors: Ping Zhang, Chuang He, Damian Przestacki, Yu-Cun GuDeadline: 5 October 2026
Topic in
Aerospace, Applied Sciences, Astronautics, Coatings, J. Compos. Sci., JMMP, Materials, Polymers
Advanced Materials and Manufacturing for Extreme Environments in Energy and Aerospace
Topic Editors: Richard E. Wirz, Chih-Hung (Alex) Chang, Tianyi Chen, Somayeh Pasebani, Dong Lin, Devin J. Roach, Jesse A. RodriguezDeadline: 31 October 2026
Topic in
Chemosensors, JMMP, Materials, Nanomaterials, Sensors
Functional Materials for Chemical Sensing and Environmental Sustainability: Trends, Concepts and Applications
Topic Editors: Michele Penza, Guanying Chen, Anming HuDeadline: 31 December 2026
Topic in
Materials, Micromachines, Actuators, JMMP, Electronics, Sensors
Magnetostrictive Sensors: Principle, Design and Applications
Topic Editors: Yisong Tan, Keat Ghee Ong, Limin RenDeadline: 31 January 2027
Conferences
Special Issues
Special Issue in
JMMP
Artificial Intelligence Systems for Intelligent Manufacturing
Guest Editors: Idilia Batchkova, Gancho L. VachkovDeadline: 30 September 2026
Special Issue in
JMMP
Advanced Design, Manufacturing, and Applications of Precision Machine Tools
Guest Editor: Jun ZhaDeadline: 30 September 2026
Special Issue in
JMMP
Advances in Material Forming, 3rd Edition
Guest Editor: Chetan P. NikhareDeadline: 30 September 2026
Special Issue in
JMMP
Emerging Functional, Topological, Metamaterial, and Optimization-Based Design Approaches for Additive Manufacturing
Guest Editors: Enrico Dalpadulo, Marco ZagoDeadline: 30 September 2026