Article

Hydrothermal Corrosion Resistance of Reaction-Bonded SiC Ceramic: Synergistic Enhancement by Homogeneous MoSi2 Distribution and Residual Silicon Reduction


1
College of Materials Science and Engineering, Zhejiang University of Technology, Hangzhou 310014, China
2
Zhejiang Key Laboratory of Data-Driven High-Safety Energy Materials and Applications, Ningbo Key Laboratory of Special Energy Materials and Chemistry, Ningbo Institute of Materials Technology and Engineering, Chinese Academy of Sciences, Ningbo 315201, China
3
Qianwan Institute of CNITECH, Ningbo 315336, China
*
Authors to whom correspondence should be addressed.
Materials 2026, 19(10), 2039; https://doi.org/10.3390/ma19102039
Submission received: 21 March 2026 / Revised: 25 April 2026 / Accepted: 29 April 2026 / Published: 13 May 2026

Abstract

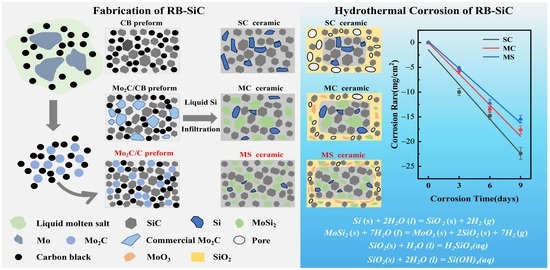
Reaction-bonded SiC (RBSC) ceramics exhibit limited hydrothermal corrosion resistance due to the presence of residual silicon. This study presents a strategy to enhance the corrosion resistance of RBSC through homogeneous incorporation of MoSi2 and concurrent reduction in residual silicon content. Three material systems were fabricated via reactive melt infiltration: conventional RBSC with a SiC/C preform (SC), a SiC–MoSi2 composite incorporating commercial Mo2C powder via physical mixing (MC), and a SiC–MoSi2 composite derived from a Mo2C/C precursor synthesized by a molten salt method (MS). The Mo2C/C composite synthesized at 1150 °C exhibited fine, uniformly distributed Mo2C particles coated on carbon black, contrasting with the agglomerated distribution in commercial Mo2C mixtures. During reactive sintering at 1600 °C, Mo2C reacted with molten Si to form MoSi2, reducing residual Si content. Sample MS achieved the lowest residual Si (8.77 ± 0.45 vol.%), followed by MC (12.43 ± 0.86 vol.%) and SC (19.17 ± 1.01 vol.%). All samples achieved near-full densification (open porosity < 0.1%), with bulk densities of 2.96 ± 0.05, 3.03 ± 0.03, and 3.07 ± 0.03 g/cm3 for SC, MC, and MS, respectively. Microstructurally, MS displayed homogeneous MoSi2 dispersion, while MC showed partial MoSi2 aggregation, and SC contained continuous residual Si regions. Hydrothermal corrosion tests at 345 °C and 15 MPa for 9 days demonstrated that corrosion resistance followed the order MS > MC > SC. After 9 days, weight loss was 22.3970 ± 1.2059 mg/cm2 (SC), 17.6370 ± 0.8266 mg/cm2 (MC), and 15.4347 ± 0.7807 mg/cm2 (MS), with corrosion depths of 393.17 ± 27.46, 267.40 ± 24.44, and 224.60 ± 25.13 μm, respectively. The enhanced performance of MS arises from two synergistic factors: reduced residual Si minimizes large corrosion pores, while uniform distribution of MoSi2 facilitates the formation of a stable, dissolution-resistant composite oxide layer composed of MoO3 and SiO2, in which MoO3 restrains excessive dissolution of SiO2 through a pinning effect. These findings demonstrate that combining residual Si reduction with homogeneous MoSi2 incorporation via molten salt-synthesized precursors offers an effective strategy for improving hydrothermal corrosion resistance of reaction-bonded SiC-based materials for applications in high-temperature and high-pressure aqueous environments such as nuclear water reactors.

Graphical Abstract

1. Introduction

Silicon carbide (SiC) is an advanced ceramic with exceptional comprehensive properties, including excellent high-temperature mechanical strength, oxidation resistance, corrosion resistance, and radiation resistance. It is widely used in high-end manufacturing, optoelectronics, nuclear energy, advanced composites, and other high-tech fields [1,2,3,4,5,6,7,8,9]. In particular, SiC exhibits superior neutron irradiation resistance, low neutron absorption cross-section, minimal mechanical degradation under irradiation, and low volume swelling, making it an ideal material for key components in nuclear reactors [10,11,12,13,14,15,16]. Consequently, SiC-based materials, especially SiC fiber-reinforced SiC composites (SiCf/SiC), have emerged as leading candidates for accident-tolerant fuel (ATF) cladding in pressurized water reactors (PWRs).
Among various fabrication routes for SiC ceramics, reaction-bonded silicon carbide (RBSC) prepared via reactive melt infiltration (RMI) offers distinct advantages, including low processing cost, short fabrication cycles, near-net-shape capability with minimal shrinkage, and the ability to produce complex-shaped components [17,18,19,20,21]. During RMI, molten silicon infiltrates a porous SiC/C preform and reacts with carbon to form secondary β-SiC, resulting in nearly fully dense materials with open porosity approaching zero. However, an inherent limitation of this process is the unavoidable presence of residual free silicon, typically ranging from 15 to 20 vol.%, which remains unreacted in the final microstructure [22,23,24,25].
In PWR environments, fuel cladding materials are subjected to high-temperature and high-pressure water (typically ∼300–360 °C, ∼15 MPa) over extended service periods. Under such hydrothermal conditions, the residual silicon in RBSC is preferentially attacked, undergoing oxidation to form amorphous SiO2, which subsequently dissolves as soluble silicate species (e.g., H2SiO3 or Si(OH)4) [26,27,28]. This dissolution process creates interconnected pores and corrosion channels, allowing further ingress of the corrosive medium and accelerating degradation of the material. Therefore, improving the hydrothermal corrosion resistance of RBSC by alleviating the detrimental effects associated with residual silicon is critical to its application as nuclear fuel cladding in pressurized water reactors (PWRs).
One promising strategy to address this challenge is to convert the residual silicon into more chemically stable phases. Reported approaches for controlling residual silicon in the literature, including powder gradation optimization, CVD pyrolytic carbon coating, and carbon precursor infiltration pyrolysis (CPIP), primarily focus on improving mechanical properties and lack targeted design and optimization for hydrothermal corrosion resistance [29,30,31]. Molybdenum disilicide (MoSi2) is particularly attractive for this purpose due to several advantageous characteristics. Molybdenum possesses a low thermal neutron absorption cross-section, which is essential for maintaining neutron economy in nuclear reactors [32,33,34,35,36]. Furthermore, MoSi2 exhibits outstanding oxidation resistance even at elevated temperatures, attributed to the formation of a protective and self-healing SiO2 glass layer upon exposure to oxidizing environments [37,38]. Indeed, MoSi2 is widely employed in high-temperature heating elements and protective coatings for refractory metals, demonstrating its reliability under extreme thermal and corrosive conditions [39,40,41]. By introducing Mo-containing precursor like Mo2C into the RBSC preform, the infiltrated molten silicon can react with it to form MoSi2, thereby reducing the residual silicon content while simultaneously incorporating a more corrosion-resistant silicide phase.
The effectiveness of this strategy, however, depends critically on the homogeneity and fineness of the Mo2C distributed within the preform. Commercial Mo2C powders typically exhibit coarse particle sizes and broad size distributions. Moreover, the significant density disparity between Mo2C (ρ = 9.18 g/cm3) and carbon black (ρ = 1.8 g/cm3) readily leads to powder segregation and agglomeration during mixing. Such microstructural inhomogeneities inevitably result in the formation of coarse MoSi2 grains, uneven phase distribution, and increased amounts of unreacted residual silicon, all of which compromise the hydrothermal corrosion resistance of the final material. The molten salt synthesis method offers unique advantages for overcoming these limitations, enabling the preparation of fine, uniformly coated composite powders through a dissolution–reprecipitation mechanism in a liquid salt medium [42,43,44,45]. This approach has been successfully employed to synthesize various carbide and MAX phase powders with refined microstructures. Furthermore, compared with the complicated procedures of conventional coating processes, the molten salt method features simpler operation and a shorter flow, thereby showing greater potential for industrial applications [30].
In this study, three material systems were fabricated via reactive melt infiltration to systematically investigate the effect of MoSi2 incorporation and residual silicon reduction on hydrothermal corrosion resistance: (i) conventional RBSC with a SiC/C preform (SC); (ii) a SiC–MoSi2 composite incorporating commercial Mo2C powder via physical mixing (MC); and (iii) a SiC–MoSi2 composite derived from a Mo2C/C precursor synthesized by the molten salt method, subsequently mixed with SiC powder to form the preform (MS). The phase composition, densification behavior, microstructural evolution, residual silicon content, and hydrothermal corrosion performance at 345 °C and 15 MPa were systematically evaluated. Through comparative analysis, the underlying mechanisms by which homogeneous MoSi2 distribution and reduced residual silicon enhance hydrothermal corrosion resistance were elucidated. It should be noted that while this work focuses on monolithic SiC ceramics as a model system, the findings are expected to provide fundamental insights and technical guidance for advancing RMI-processed SiCf/SiC composites as potential accident-tolerant fuel cladding materials for future pressurized water reactors. This study ultimately validates the core hypothesis that uniformly distributed MoSi2 coupled with low residual silicon synergistically promotes the generation of a dense, stable, dissolution-resistant oxide scale, which efficiently restricts hydrothermal degradation and improves the service durability of SiC-based materials.

2. Experimental Procedure

2.1. Synthesis of Mo2C/C Composite Powder via Molten Salt Method

Carbon black (D50 = 20 nm, Qinhuangdao Yinuo High-Tech Material Development Co., Ltd., Qinhuangdao, China) and molybdenum powder (99.5% purity, D50 = 2 μm, Shanghai Macklin Co., Ltd., Shanghai, China) were used as starting materials. Sodium chloride (NaCl, ≥99.5 wt.%, Shanghai Aladdin Bio-Chem Technology Co., Ltd., Shanghai, China) and potassium chloride (KCl, ≥99 wt.%, Shanghai Aladdin Bio-Chem Technology Co., Ltd., Shanghai, China) served as the molten salt medium. The molten salt (NaCl:KCl = 1:1 in molar ratio) and raw materials (Mo:C = 1:6 in molar ratio) were uniformly mixed using an agate mortar and pestle at a mass ratio of 2:1 (salt:raw materials). The resulting mixture was poured into an alumina crucible and placed in an alumina tube furnace. The mixture was heated to target temperatures (850, 950, 1050, and 1150 °C) and held for 4 h under flowing argon to synthesize uniformly coated Mo2C on the carbon black surface via the molten salt method.
The as-obtained product, consisting of the synthesized powder and residual salts, was then immersed in deionized water and heated in a water bath at 70 °C with rotary stirring for 60 min to fully dissolve the salts, followed by vacuum filtration using a Büchner funnel and filter paper. This washing–filtration process was repeated three times to completely remove residual salts. Finally, the washed powders were dried in an oven at 100 °C for 24 h to obtain the Mo2C/C composite powder. The Mo/C molar ratio of 1:6 has been verified in preliminary experiments, and the Mo2C/C composite powder prepared by the molten salt method exhibits good reproducibility.

2.2. Fabrication of SiC Ceramic and SiC-MoSi2 Composites

For the preparation of reaction-bonded SiC ceramics and SiC–MoSi2 composites, the following raw materials were used: α-SiC powder (average particle size 0.5 μm, Qinhuangdao Yinuo High-Tech Material Development Co., Ltd., Qinhuangdao, China), silicon particles (particle size 1–3 mm, purity 99.99%, Qinhuangdao Yinuo High-Tech Material Development Co., Ltd., Qinhuangdao, China), commercial Mo2C powder (particle size 1–3 μm, purity 99.99%, Qinhuangdao Yinuo High-Tech Material Development Co., Ltd., Qinhuangdao, China), Mo2C/C composite powder synthesized via the molten salt method, carbon black, polyvinylpyrrolidone (PVP, Shanghai Aladdin Bio-Chem Technology Co., Ltd., Shanghai, China), and polyvinyl butyral (PVB, Aviation Grade, Sinopharm Chemical Reagent Co., Ltd., Shanghai, China).
Three different powder formulations were prepared: (1) Sample SC: 80 wt.% α-SiC and 20 wt.% carbon black; (2) Sample MC: 80 wt.% α-SiC, 7.8 wt% carbon black, and 12.2 wt.% commercial Mo2C powder; (3) Sample MS: 80 wt.% α-SiC and 20 wt.% Mo2C/C composite powder synthesized by the molten salt method. This formulation was designed to have the same nominal composition as Sample MC.
Each powder mixture was dispersed in ethanol with the addition of 2 wt.% PVP (based on total powder mass) as dispersant and 1 wt.% PVB as binder. The slurries were mixed in polyethylene bottles using zirconia balls as milling media on a roller mill for 8 h. After ball milling, the mixed slurries were dried using a vacuum rotary evaporator at 70 °C. The dried cakes were crushed and sieved, and the resulting powder mixtures were uniaxially dry-pressed in a stainless-steel mold, followed by cold isostatic pressing (CIP) at 200 MPa for 5 min.
The green compacts were subjected to a vacuum debinding treatment at 900 °C for 1 h to remove organic additives, and the green density was determined as follows: SC: 1.72 ± 0.04 g/cm3; MC: 1.76 ± 0.02 g/cm3; MS: 1.78 ± 0.03 g/cm3. Subsequently, the green bodies were infiltrated with molten silicon at 1600 °C for 2 h under vacuum (<30 Pa) in a graphite furnace. The resulting RB-SiC ceramic and RB-SiC–MoSi2 composites were ground and polished to a 1 μm finish using diamond suspensions.

2.3. Characterizations

The bulk density (ρ) and porosity (p) of the composite ceramics prepared by RMI were measured using Archimedes’ principle. Equations (1) and (2) were used to calculate ρ and p, respectively. The calculation methods for these values are as follows:
ρ = m d ρ w m w m s
P = m w m d m w m s × 100 %
where ρw is the density of deionized water, md is the dry mass of the sample, mw is the saturated wet mass in air, and ms is the suspended mass measured in water.
The residual silicon content in the ceramic samples was quantitatively determined by an alkali etching method. Previous studies have demonstrated that SiC and MoSi2 exhibit excellent alkali corrosion resistance [46,47,48]. Specifically, samples were first thinned to a thickness of 500 μm, then immersed in a 30 wt.% NaOH solution and heated in a water bath at 70 °C for three days. This mild alkali etching selectively removes residual Si without attacking other phases such as SiC or MoSi2 in the reactive sintered ceramic samples. The reaction between residual Si and NaOH solution can be described as Equation (3):
Si(s) + 2NaOH(aq) + H2O(l) = Na2SiO3(aq) + 2H2(g)
After alkali etching, the volume fraction of residual Si was estimated from the mass change using the following formula:
Vsi = ρ ( m 1 m 2 ) ρ S i · m 1 × 100 %
where m1 and m2 are the masses before and after alkali etching, ρ is the density of the reactive sintered sample, and ρSi is the density of silicon (2.33 g/cm3).
Hydrothermal corrosion tests were conducted in an autoclave (FGD, Dalian Tongchan Autoclave Manufacturing Co., Ltd., Dalian, China) using ultrapure water under conditions of 345 °C and 15 MPa for a total duration of 9 days. During the corrosion experiment, samples were taken out every 3 days to record mass changes. Three parallel tests were conducted for each sample. The mass change per unit area (∆w) was calculated as in Equation (5):
w = m t m 0 s × 100 %
where ∆w is the mass change per unit area (g/cm2), m0 is the initial mass (g), mt is the mass after corrosion time t (g), and s is the surface area of the sample (cm2).
Phase identification was conducted by X-ray diffraction (XRD; D8 Advance, Bruker AXE, Karlsruhe, Germany). Microstructures and elemental composition were analyzed using field-emission scanning electron microscopy (FE-SEM; Quanta 250 FEG, FEI, Hillsboro, OR, USA) equipped with an energy-dispersive spectrometer (EDS). The chemical bonding states of elements in the ceramic samples were analyzed by X-ray photoelectron spectroscopy (XPS; Axis Supra, Kratos Analytical Ltd., Tokyo, Japan). The binding energy of all high-resolution XPS spectra was calibrated by referencing the characteristic C 1s peak of surface contamination carbon at 284.8 eV to eliminate the charging effect.

3. Results and Discussion

3.1. Synthesis and Characterization of Mo2C/C Composite Powder

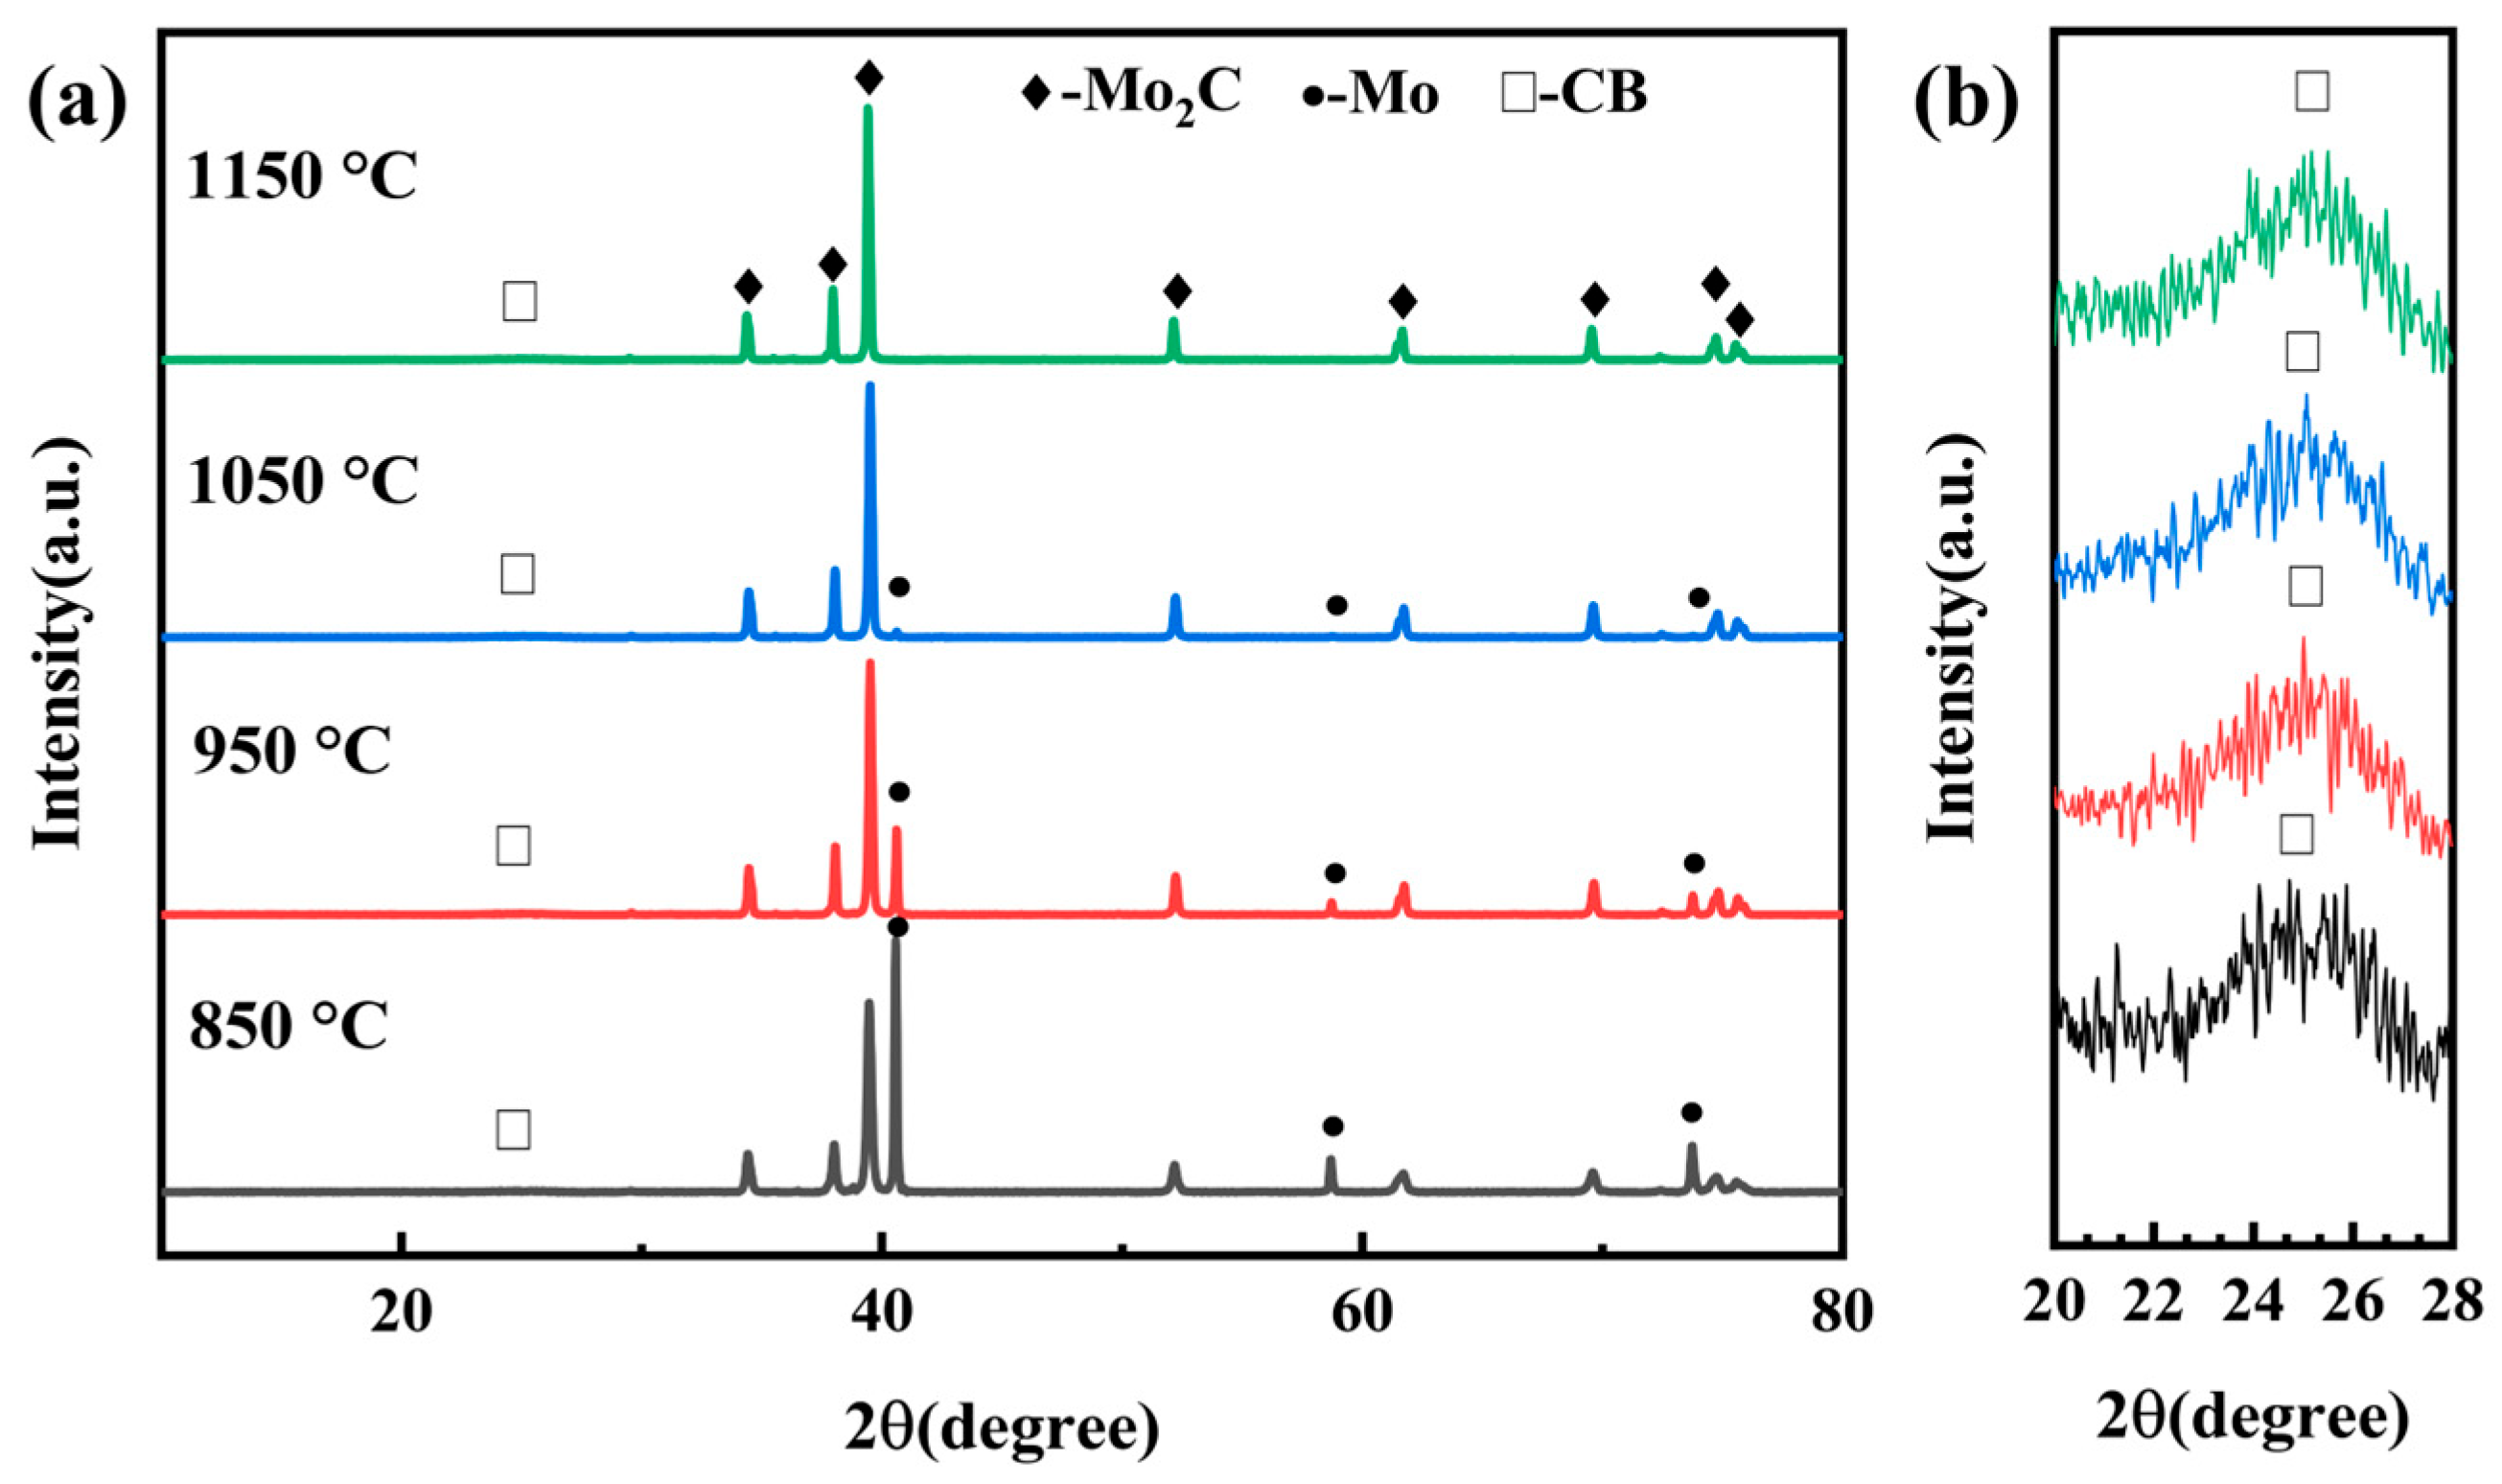
Figure 1 shows the X-ray diffraction patterns of the powder products synthesized via the molten salt method at various temperatures (850–1150 °C) for 4 h. In all four samples, Mo2C is identified as the dominant crystalline phase. Broad weak peaks located at 2θ angles of 24–26° are also observed, which are characteristic of turbostratic carbon and correspond to the residual amorphous carbon black (Figure 1b). Additionally, diffraction peaks corresponding to metallic Mo appear in the products synthesized at 850–1050 °C, and their intensity decreases markedly with increasing synthesis temperature. When the temperature reaches 1150 °C, the Mo peaks disappear completely, indicating full conversion of the molybdenum reactant.
These results demonstrate that Mo2C can be effectively synthesized via the molten salt method, with the optimal temperature being 1150 °C, where the metallic Mo is completely consumed. The formation of Mo2C proceeds through the following reaction:
2Mo(s) + C(s) = Mo2C(s)
The molten salt provides a liquid medium that facilitates reaction (6). The melting points of NaCl and KCl are approximately 801 °C and 770 °C, respectively, and their eutectic temperature is 657 °C. Since the synthesis temperatures employed in this study (850–1150 °C) exceed this eutectic point, the NaCl–KCl mixture forms a homogeneous liquid phase. This molten salt medium promotes the reaction kinetics through a dissolution–reprecipitation mechanism, accelerating the conversion of Mo and C into Mo2C.
As the synthesis temperature increases, the viscosity of the molten salt medium further decreases, enhancing mass transport and thereby improving the efficiency of the dissolution–reprecipitation process. At 1150 °C, the complete disappearance of metallic Mo diffraction peaks confirms that all Mo has been converted into Mo2C. Given that carbon black was present in excess relative to metallic Mo in the starting mixture, the final product obtained at this temperature is a composite powder consisting of Mo2C and residual carbon, as evidenced by the XRD patterns in Figure 1.
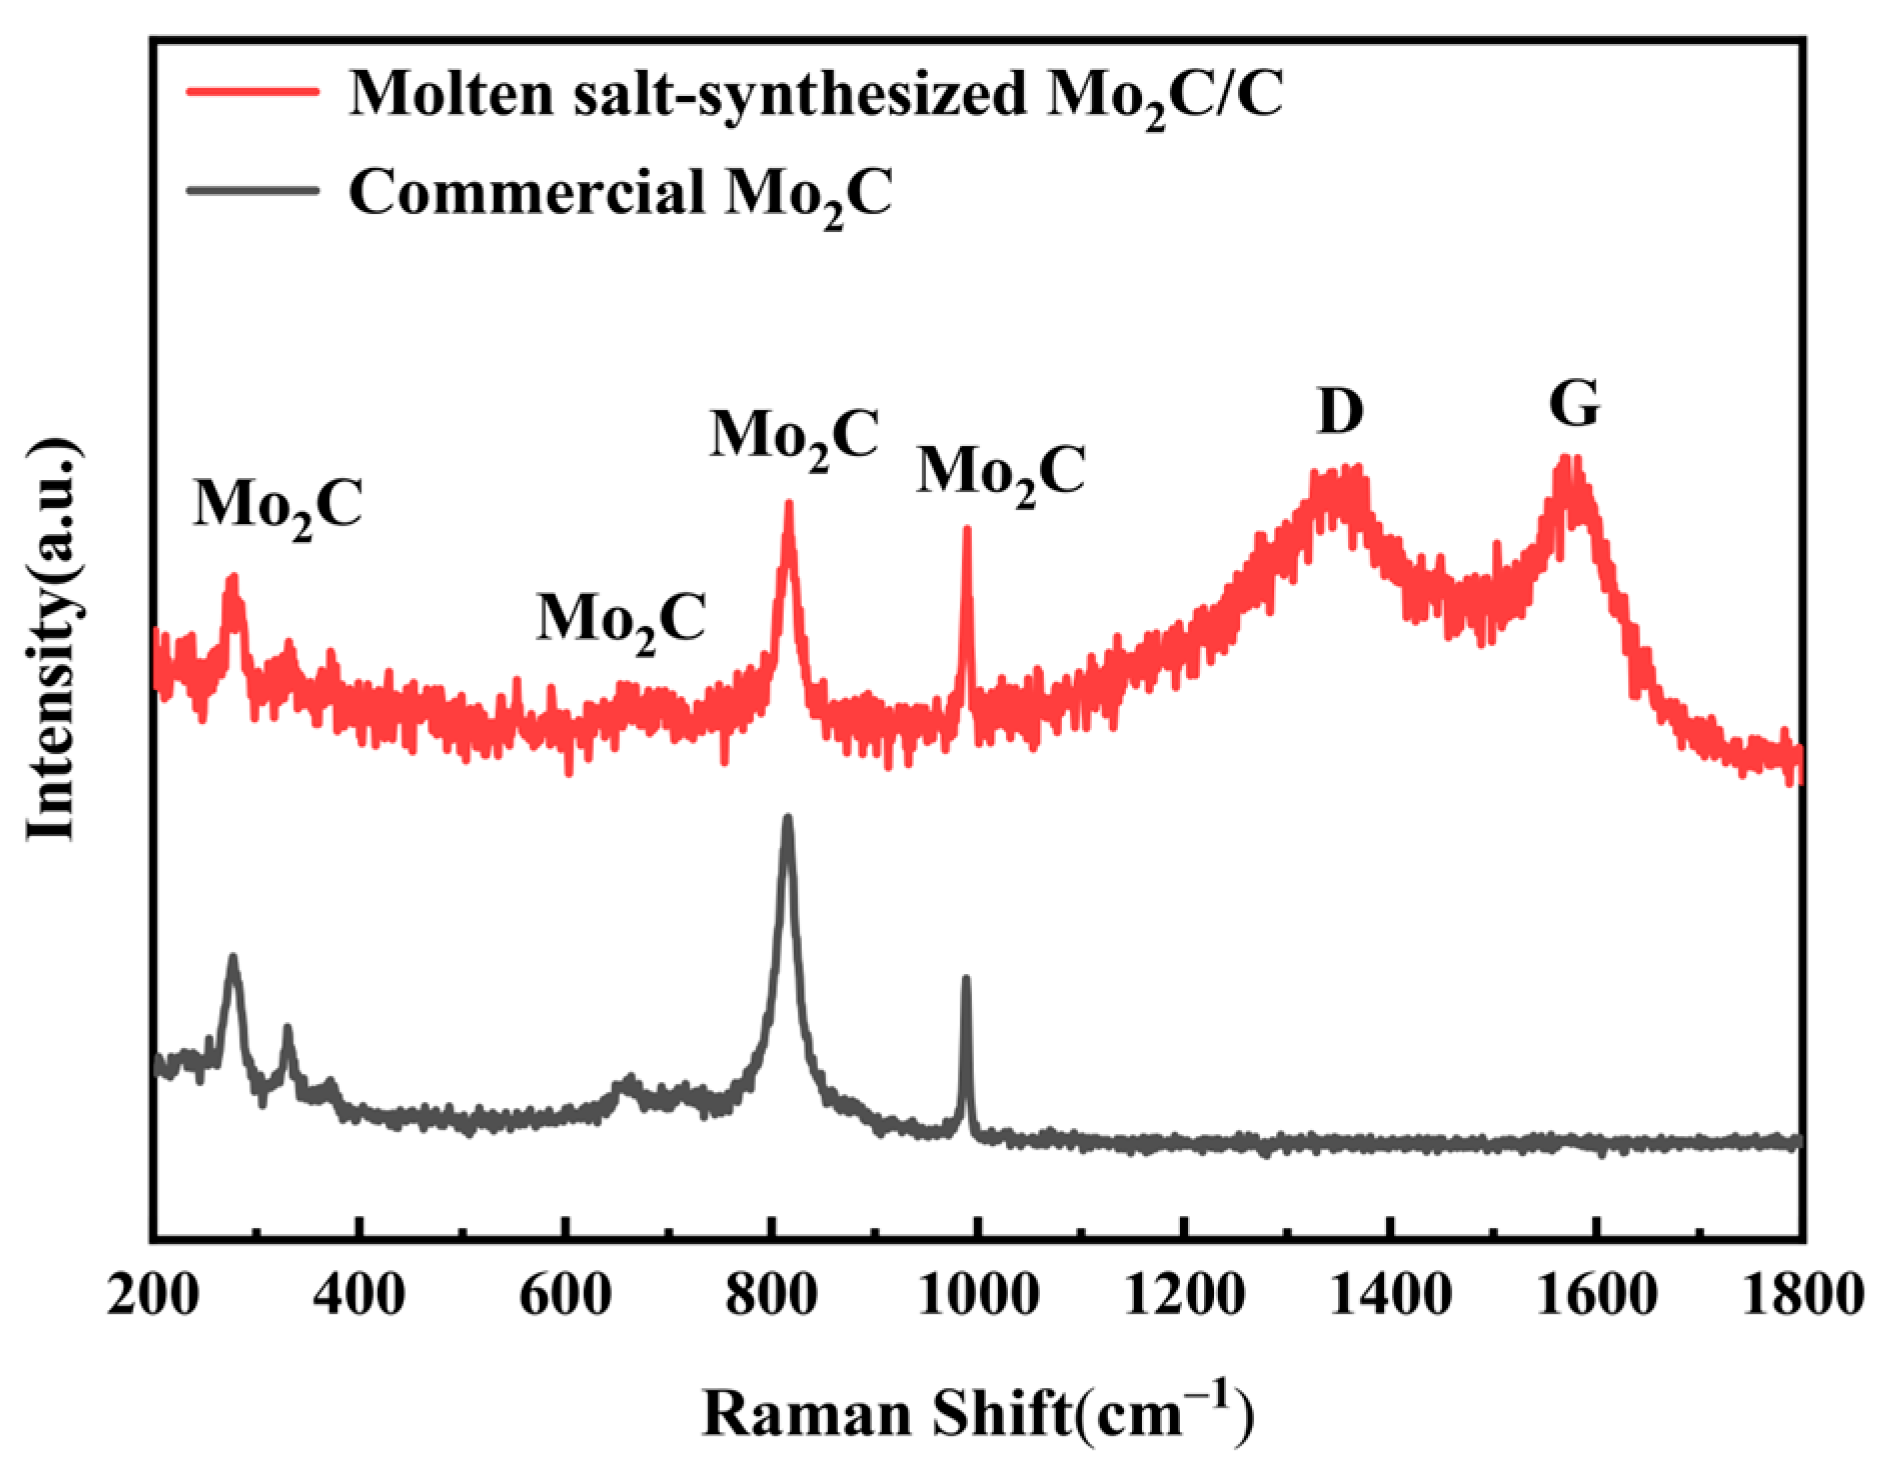
The Raman spectra of the molten salt-synthesized Mo2C/C composite (Mo/C molar ratio = 1/6) and commercial Mo2C are shown in Figure 2. Both samples exhibit characteristic peaks of Mo2C at 284, 660, 818, and 989 cm−1, confirming the successful formation of the Mo2C phase. Only the Mo2C/C composite displays distinct D (~1345 cm−1) and G (~1583 cm−1) bands, which are attributed to residual carbon [49]. No signals corresponding to metallic Mo are detected, indicating that the metallic Mo precursor is completely converted to Mo2C, while the excess unreacted carbon forms the Mo2C/C composite.
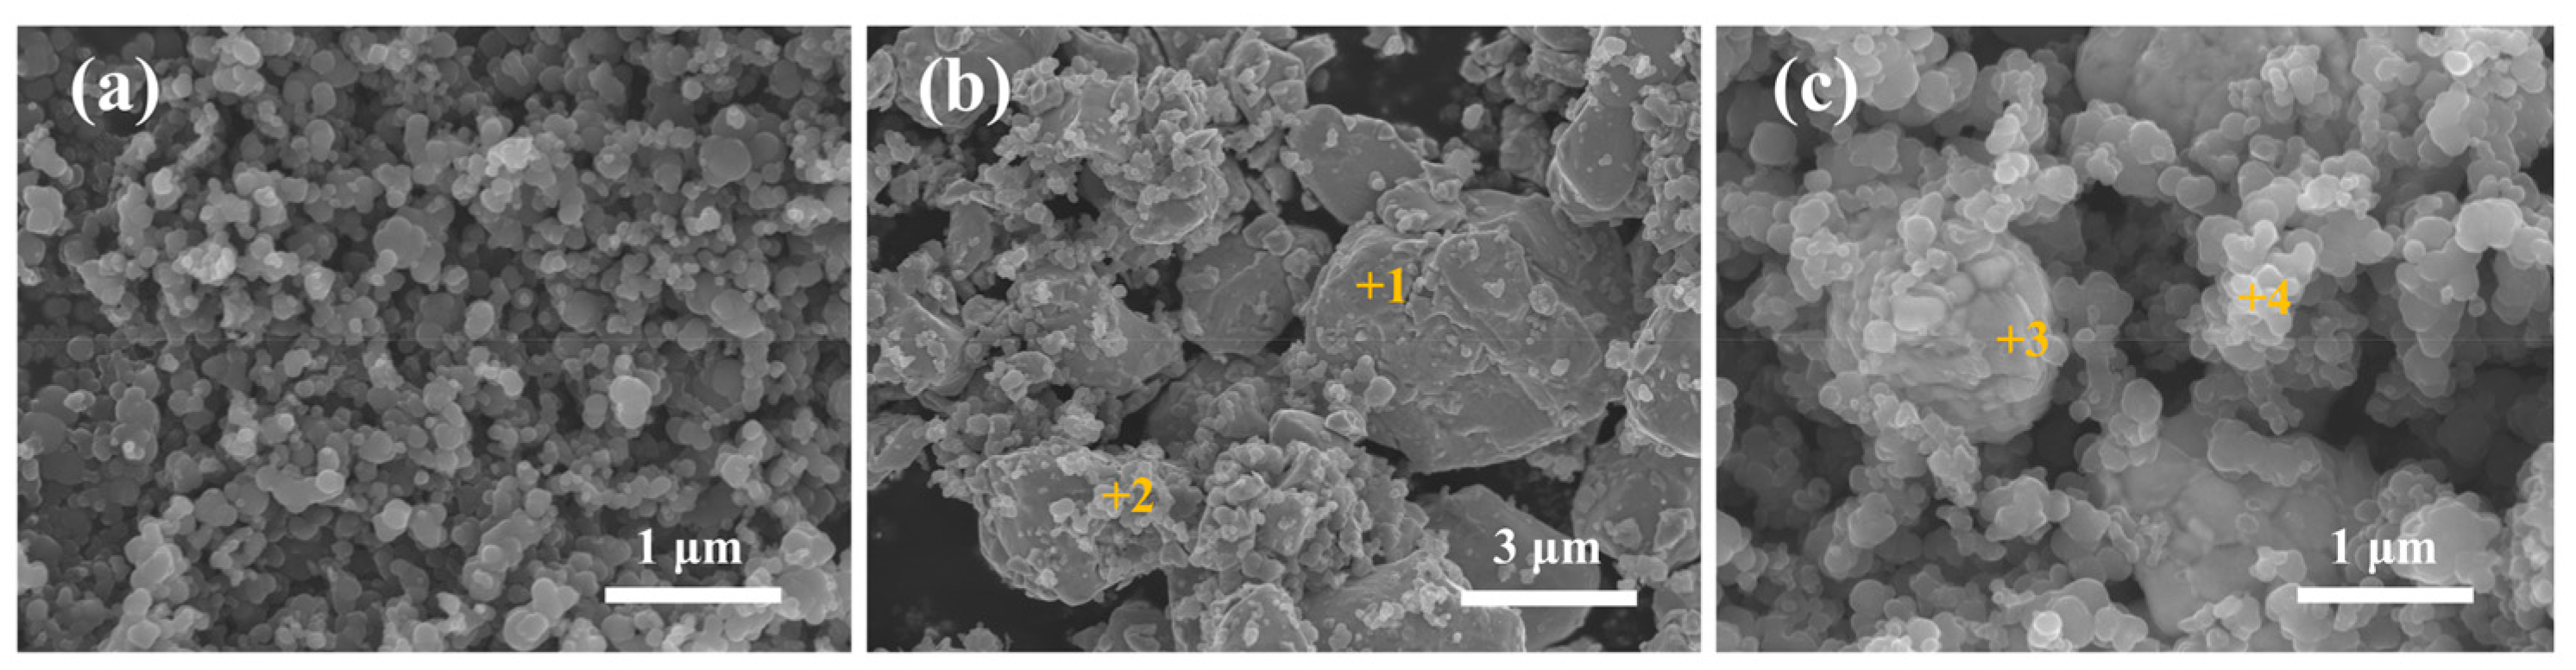
Figure 3 compares the SEM morphologies of the raw carbon black, a physical mixture of carbon black and commercial Mo2C powder, and the Mo2C/C composite powder synthesized via the molten salt method at 1150 °C. The raw carbon black (Figure 3a) exhibits a uniform spherical nanoparticle morphology with an average diameter of approximately 20 nm. In the physical mixture (Figure 3b), both spherical nanoparticles (carbon black) and micron-sized particles (1–3 μm) are observed, but their distribution is inhomogeneous, with noticeable agglomeration of the carbon black nanoparticles. EDS point analysis (Table 1) confirms that the micron-sized particles correspond to Mo2C.
In contrast, the Mo2C/C composite powder synthesized by the molten salt method (Figure 3c) displays a homogeneous microstructure in which spherical carbon black nanoparticles are uniformly coated on the surface of ≈1 μm particles, with no visible agglomeration and excellent interfacial integration between the two components. EDS analysis (Table 1), together with the XRD results presented in Figure 1, confirms that the ≈1 μm particles are Mo2C.
These microstructural observations demonstrate that the Mo2C particles synthesized via the molten salt method are finer and more uniformly distributed within the carbon black matrix compared to the commercial Mo2C powder. This improved homogeneity arises from the unique synthesis mechanism: the molten salt provides a liquid medium in which Mo dissolves, migrates, and subsequently precipitates onto the carbon black surface, where it reacts according to Equation (6) to form Mo2C. Because this in situ reaction occurs directly on the carbon black surface—coupled with the relatively fine starting Mo particle size (≈2 μm) and the mild reaction conditions of the molten salt process—a highly uniform Mo2C/C composite powder with finer Mo2C particles is obtained [50].

3.2. Phase Composition and Microstructure of Reactive Sintered Composites

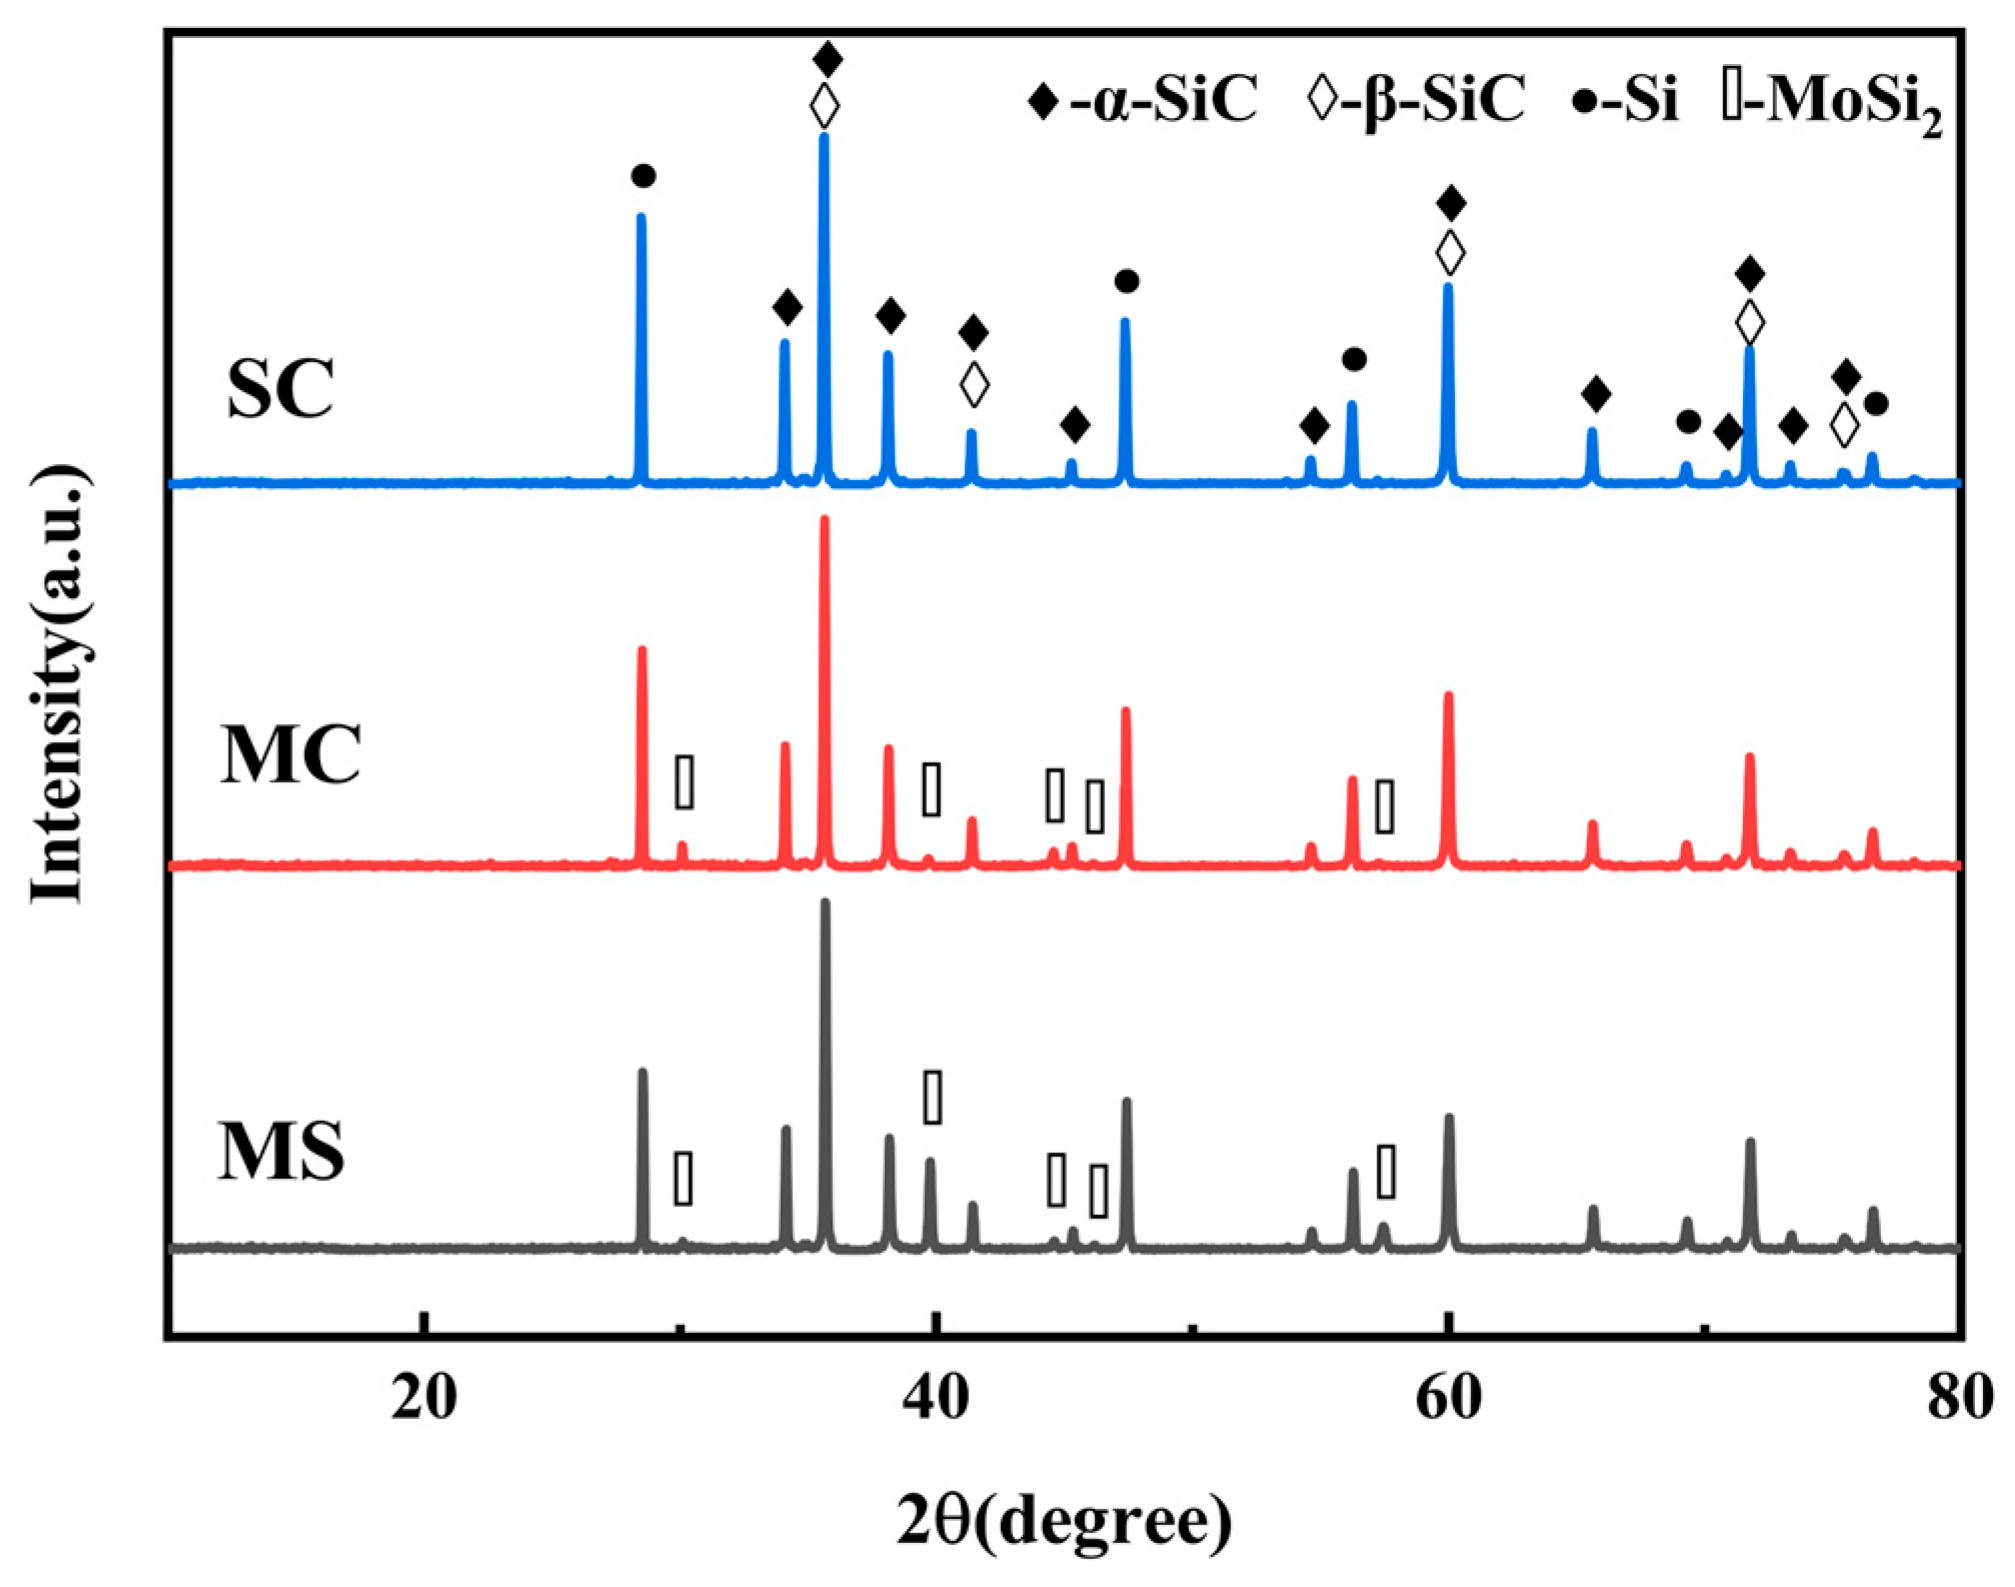
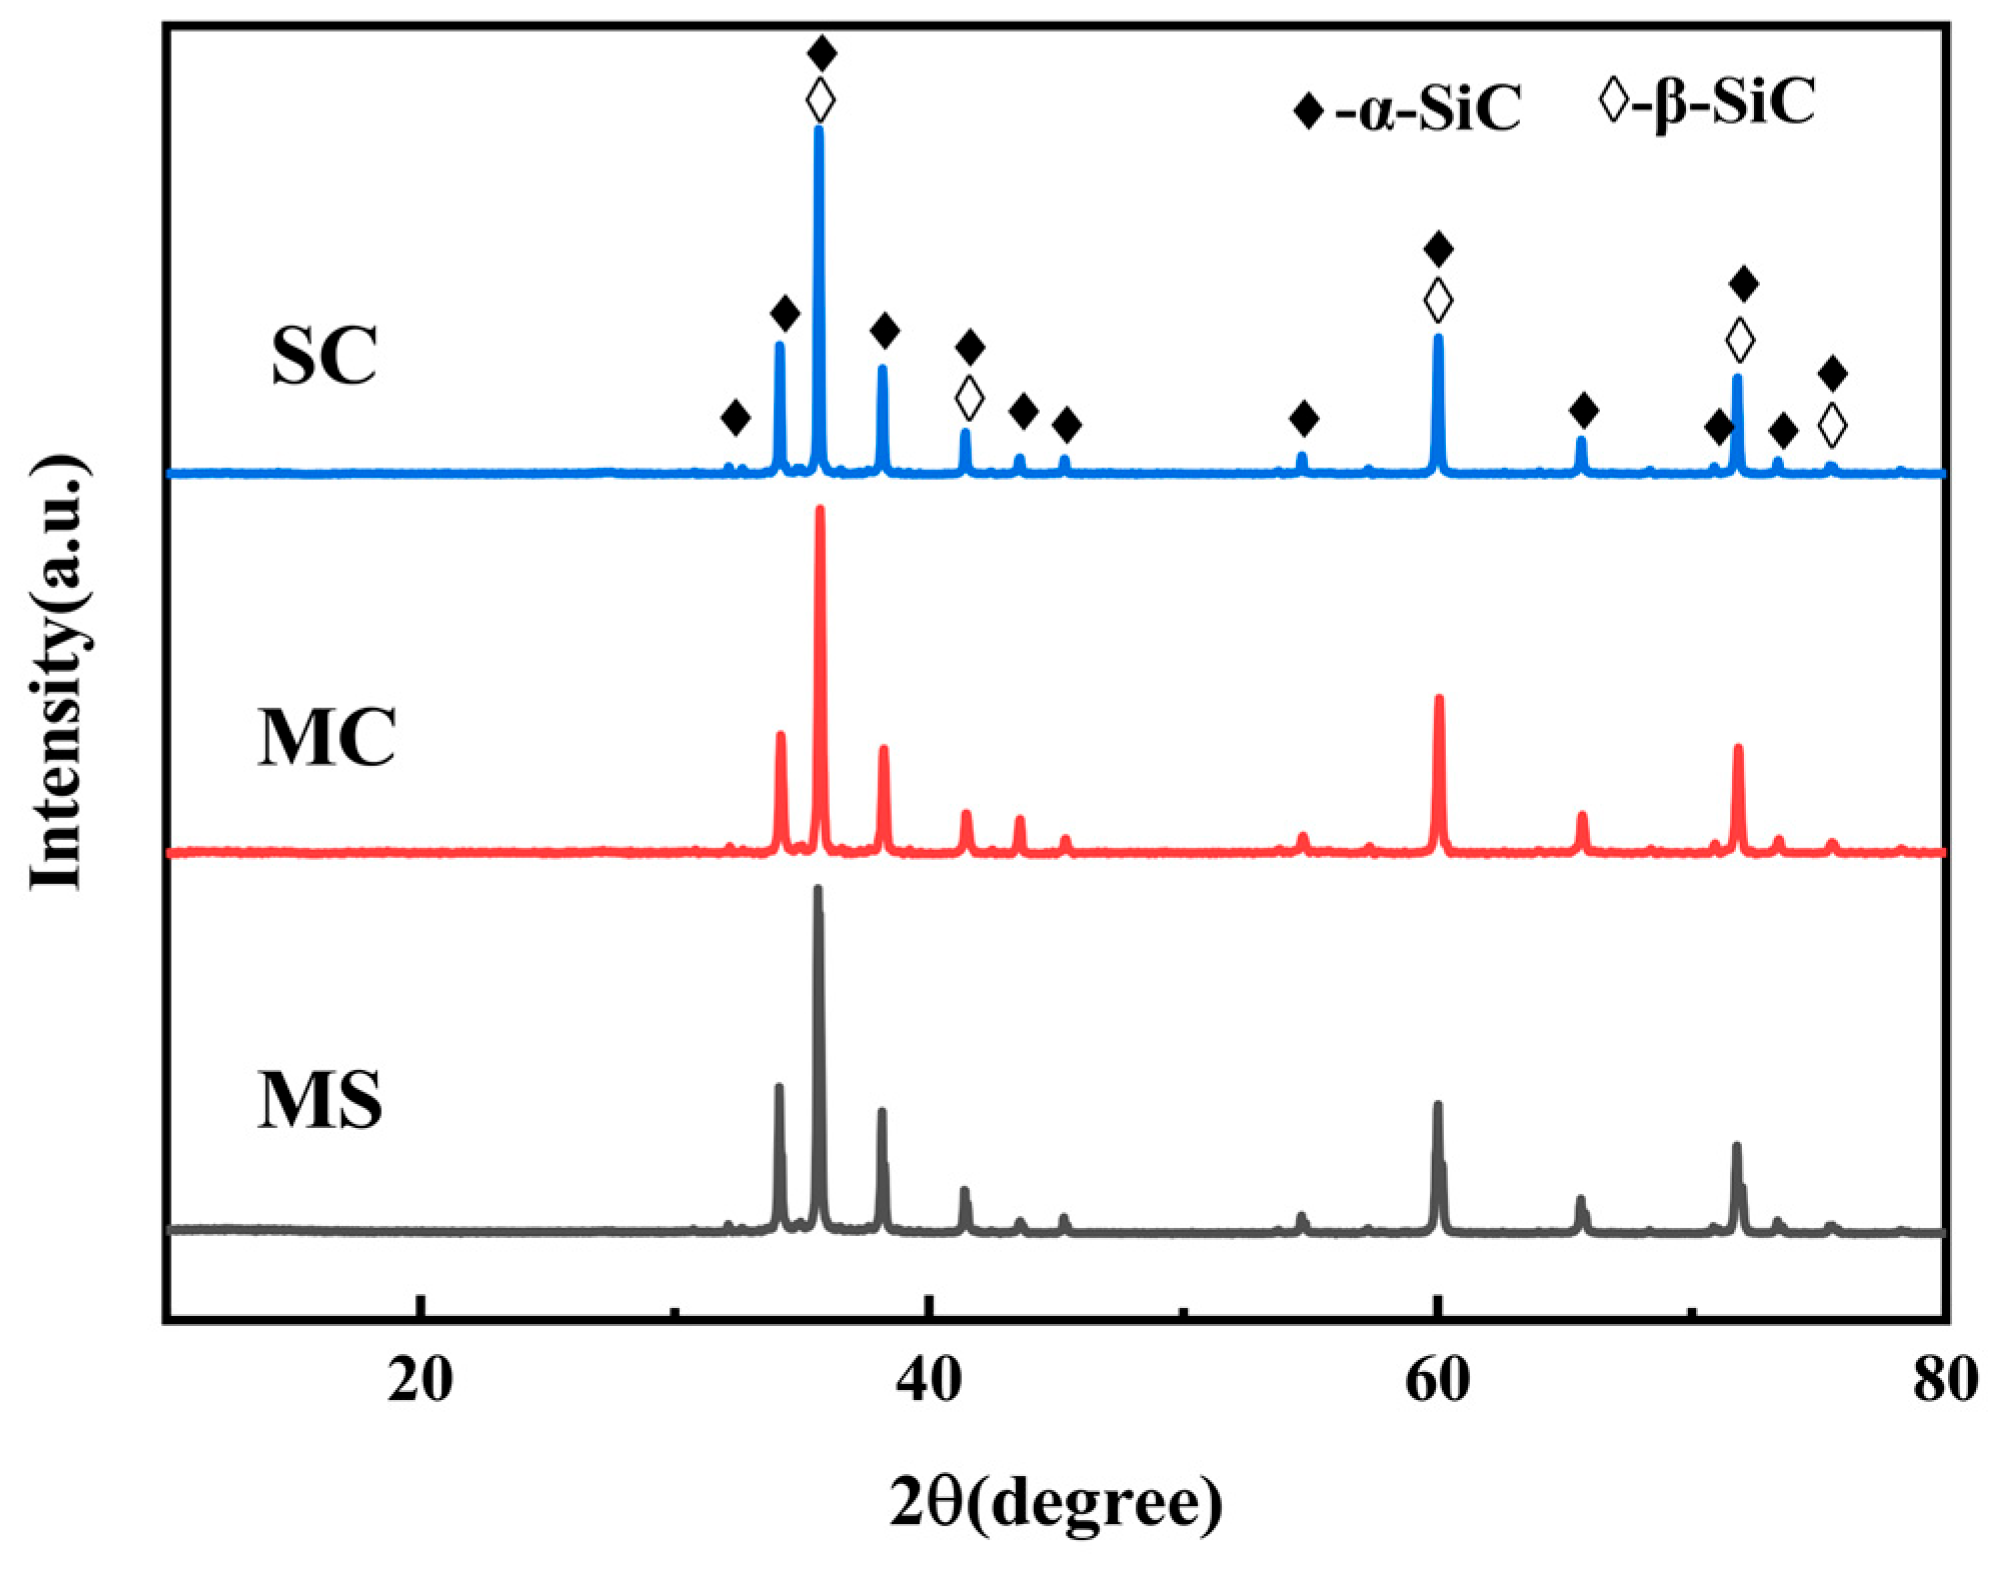
Figure 4 shows the X-ray diffraction patterns of the SiC ceramic and SiC-Mo2C composite samples after reactive sintering at 1600 °C for 2 h. In Sample SC, diffraction peaks corresponding to α-SiC (6H polytype), β-SiC (3C), and residual Si are identified, which is consistent with the typical phase composition of reaction-bonded SiC ceramics. The α-SiC originates from the starting raw material, while β-SiC is formed by the reaction between carbon black and molten silicon infiltrated into the porous SiC/C preform:
β-SiC is the low-temperature stable phase of SiC, and the sintering temperature of 1600 °C falls within the range favorable for its formation. The residual Si detected in Sample SC arises from excess molten silicon that fills the pores of the preform and remains unreacted. Quantitative analysis indicates that the residual Si content in Sample SC is as high as 19.17 ± 1.01 vol.% (Table 2).
Si(l) + C(s) → β-SiC(s)
For Samples MC and MS, diffraction peaks of both α-SiC and β-SiC are also present. However, in contrast to Sample SC, two notable differences are observed: (i) the intensity of the Si diffraction peaks is significantly reduced, and (ii) additional peaks corresponding to MoSi2 appear. Both MC and MS contain Mo2C in their porous preforms. During reactive sintering, molten silicon infiltrates the SiC–Mo2C/C preform and reacts with Mo2C to form MoSi2 according to the following reaction:
Mo2C(s) + 5Si(l) = MoSi2(s) + β-SiC(s)
Notably, compared to Sample MC, Sample MS exhibits even weaker Si diffraction peaks and stronger MoSi2 diffraction peaks. Quantitative analysis (Table 2) shows that the residual Si content decreases from 12.43 ± 0.86 vol.% in MC to 8.77 ± 0.45 vol.% in MS. This difference is attributed to the superior distribution uniformity of Mo2C within the green compact of Sample MS. The MS preform contains Mo2C/C composite powder synthesized by the molten salt method, which features finer Mo2C particles and a more homogeneous distribution compared to the physically mixed commercial Mo2C powder used in Sample MC. The finer and more uniform Mo2C particles provide a substantially larger contact area with the infiltrating molten silicon, kinetically promoting reaction (6). This enhanced reaction efficiency leads to the formation of more MoSi2 and a corresponding reduction in residual Si content.
Table 2 summarizes the densification results of the three samples. All samples achieve high densification, with open porosities below 0.1%. The bulk densities are 2.96 ± 0.05, 3.03 ± 0.03, and 3.07 ± 0.03 g/cm3 for Samples SC, MC, and MS, respectively. It is known that the theoretical densities of Si, SiC, and MoSi2 are 2.33, 3.21, and 6.28 g/cm3, respectively. Therefore, the decrease in residual Si content and the increase in MoSi2 content lead to higher sample densities, accounting for the observed density trend: SC < MC < MS.
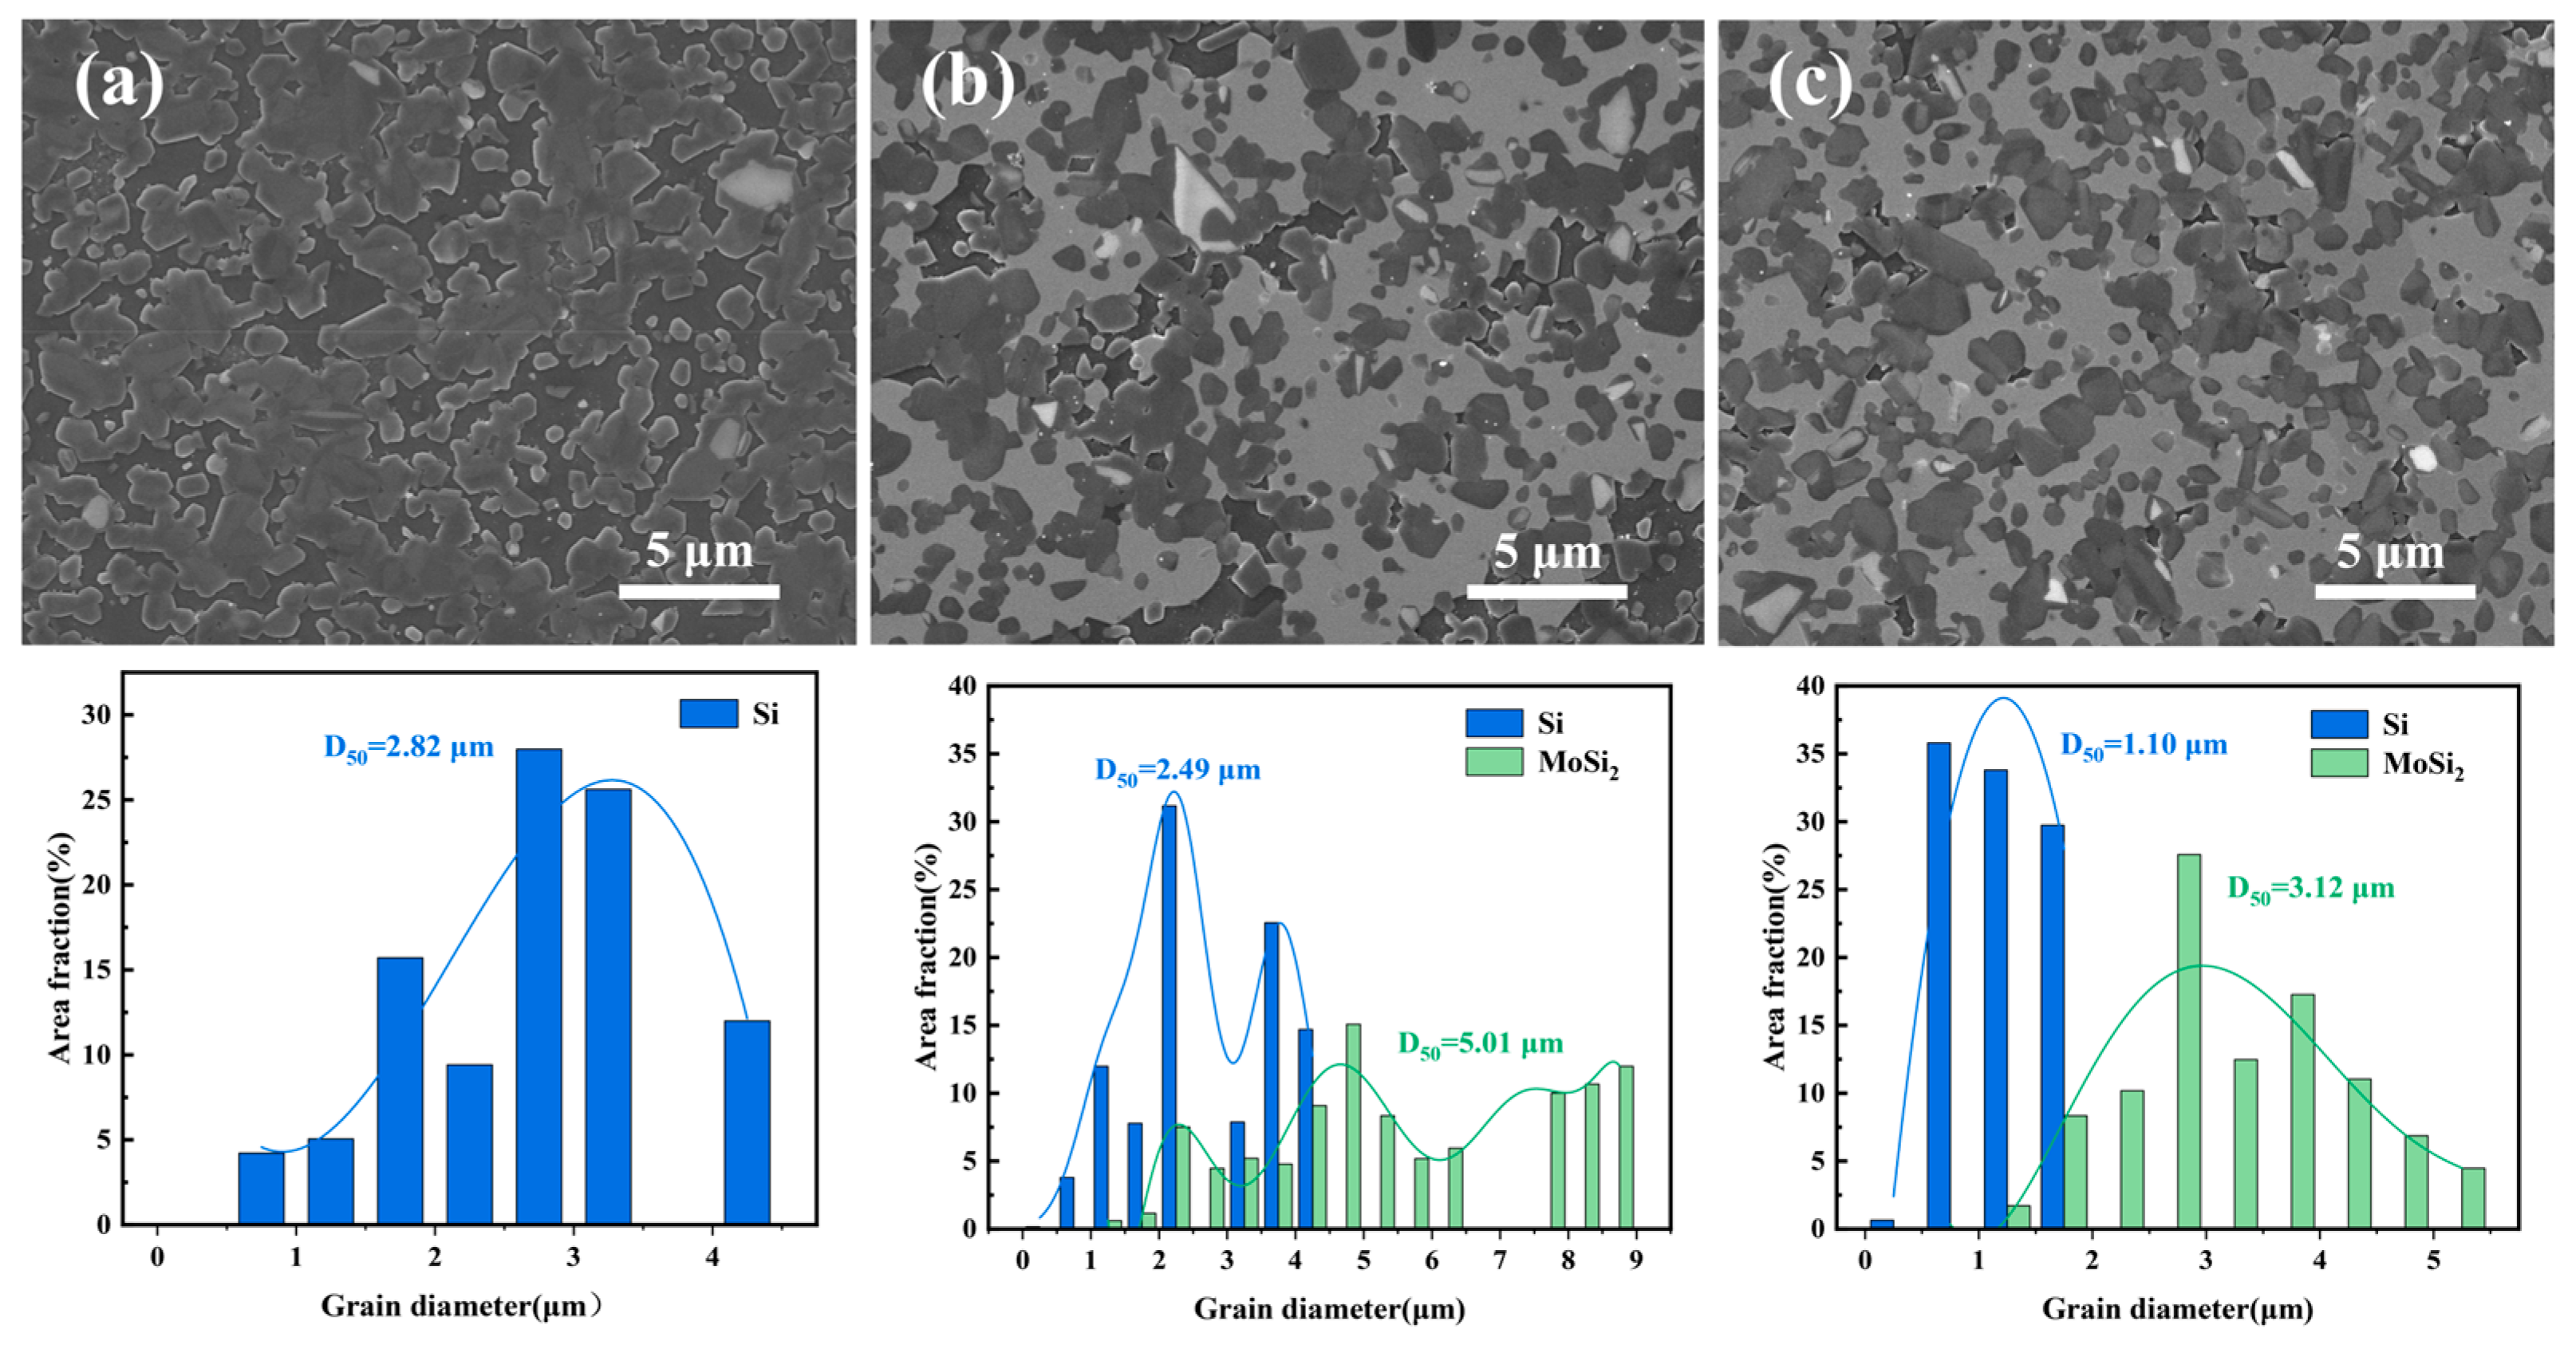
Figure 5 presents SEM images of the polished surfaces of the reactive sintered samples. All three samples exhibit highly dense microstructures, further confirming their high degree of densification. Different phases are distinguishable by their contrast levels, which arise from a mixed signal comprising secondary electrons and a minor contribution from backscattered electrons.
Sample SC (Figure 5a) consists of a continuous gray matrix composed of α-SiC and β-SiC, with discretely distributed dark regions corresponding to residual Si [51,52]. In contrast, Sample MC (Figure 5b) displays three distinct phases distinguishable by their contrast: bright gray MoSi2, light gray SiC, and minor dark regions of residual Si. Both the SiC and MoSi2 phases exhibit some degree of aggregation.
Sample MS (Figure 5c) contains the same three phases as Sample MC but exhibits significantly improved microstructural homogeneity. Quantitative statistical analysis of the size and distribution of residual Si and MoSi2 phases in the ceramic samples was performed using Image-Pro 6.0 software. The results show that the median particle size (D50) of residual Si in the MS sample is 1.10 μm, which is approximately 60% lower than that of the SC sample (2.82 μm). The D50 of MoSi2 in the MS sample is 3.12 μm, significantly smaller than that of the MC sample (5.01 μm), fully demonstrating that the phase sizes are effectively refined. Meanwhile, the particle size distributions of MoSi2 and residual Si in the MS sample are more concentrated, whereas the MC sample exhibits a broad and multi-modal distribution, indicating a higher homogeneity of phase distribution in the MS sample. Furthermore, the MC sample contains a large number of MoSi2 particles larger than 5 μm with a relatively high median particle size, providing direct quantitative evidence of obvious particle agglomeration. In contrast, the MS sample has no large agglomerated particles and exhibits better dispersion.
These microstructural observations further substantiate two key findings. First, the introduction of Mo2C into the preform effectively reduces the residual silicon content and promotes the formation of MoSi2 during reactive sintering. Second, the use of Mo2C/C composite powder synthesized by the molten salt method—characterized by finer Mo2C particles and more uniform distribution within the carbon black matrix—yields a more homogeneous microstructure and lower residual silicon content in the final reactive sintered product compared to the physically mixed commercial Mo2C powder.

3.3. Hydrothermal Corrosion Behavior

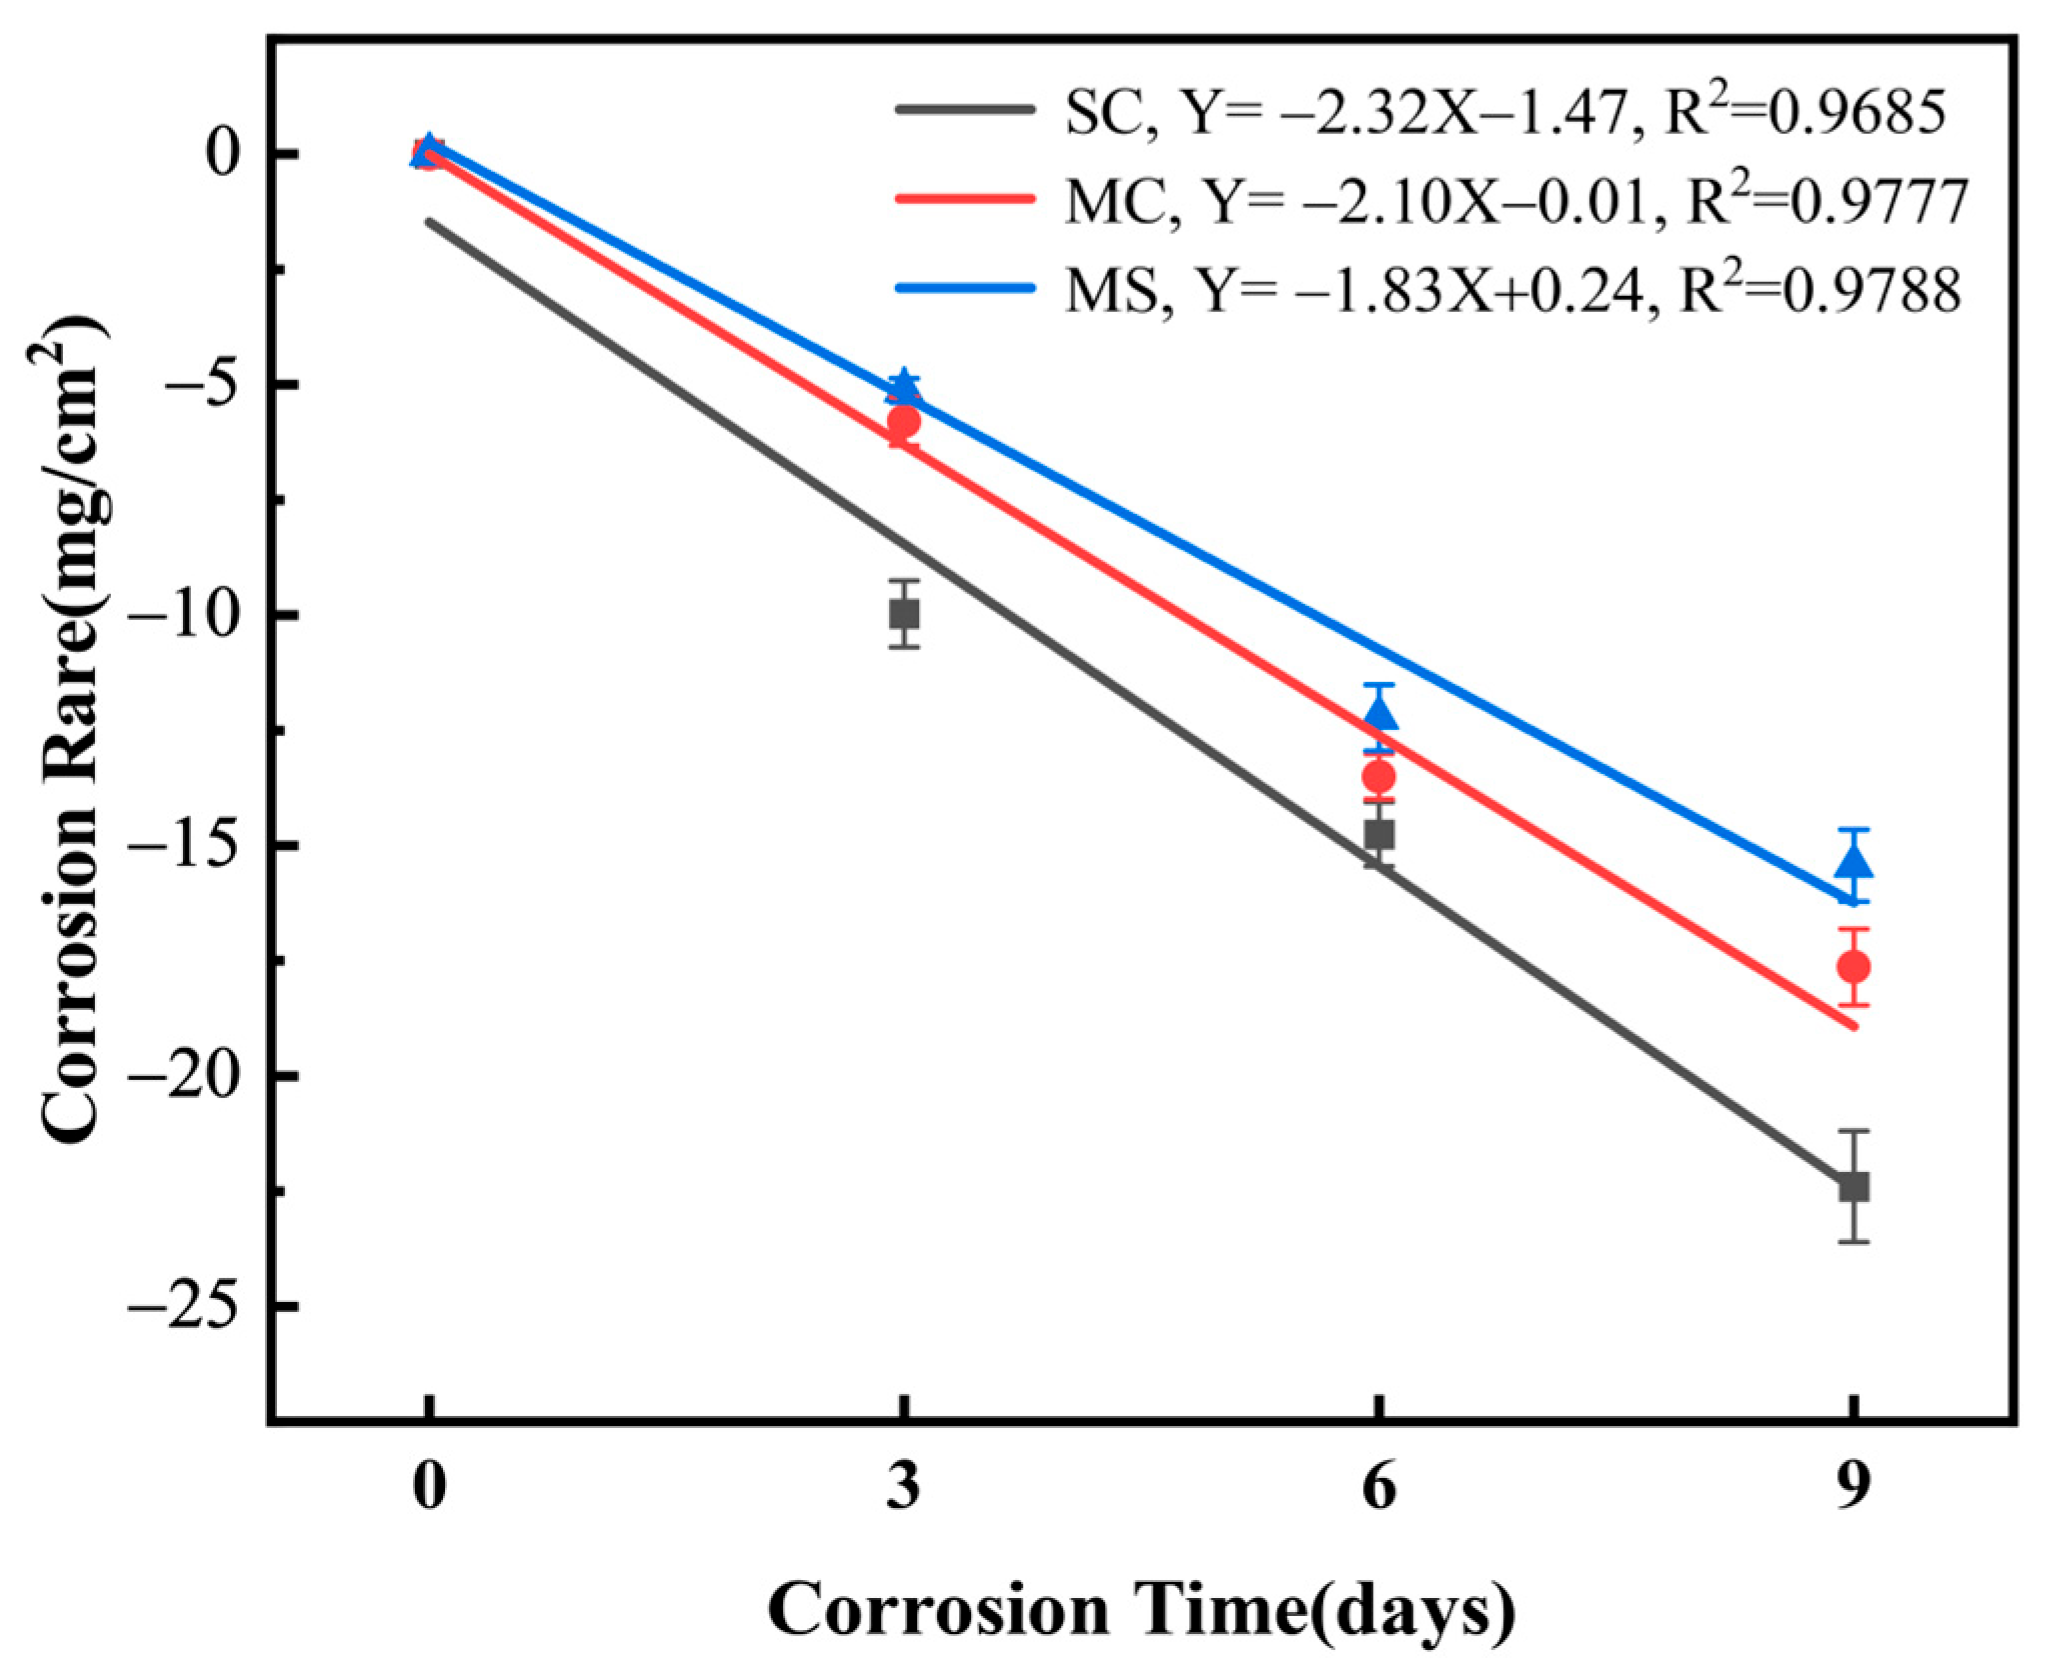
Figure 6 illustrates the corrosion weight change per unit area (∆w) of samples (SC, MC, MS) as a function of hydrothermal corrosion time. As corrosion time extended from 3 to 9 days, ∆w remained negative, with weight loss increasing approximately linearly. The ∆w values at 3, 6, and 9 days were: SC (−9.9734 ± 0.7196, −14.7575 ± 0.6968, −22.3970 ± 1.2059 mg/cm2), MC (−5.7934 ± 0.5255, −13.5051 ± 0.4871, −17.6370 ± 0.8266 mg/cm2), and MS (−5.1261 ± 0.2634, −12.2270 ± 0.7194, −15.4347 ± 0.7807 mg/cm2). Consistently, weight loss followed SC > MC > MS during corrosion, confirming hydrothermal corrosion resistance in the order SC < MC < MS.
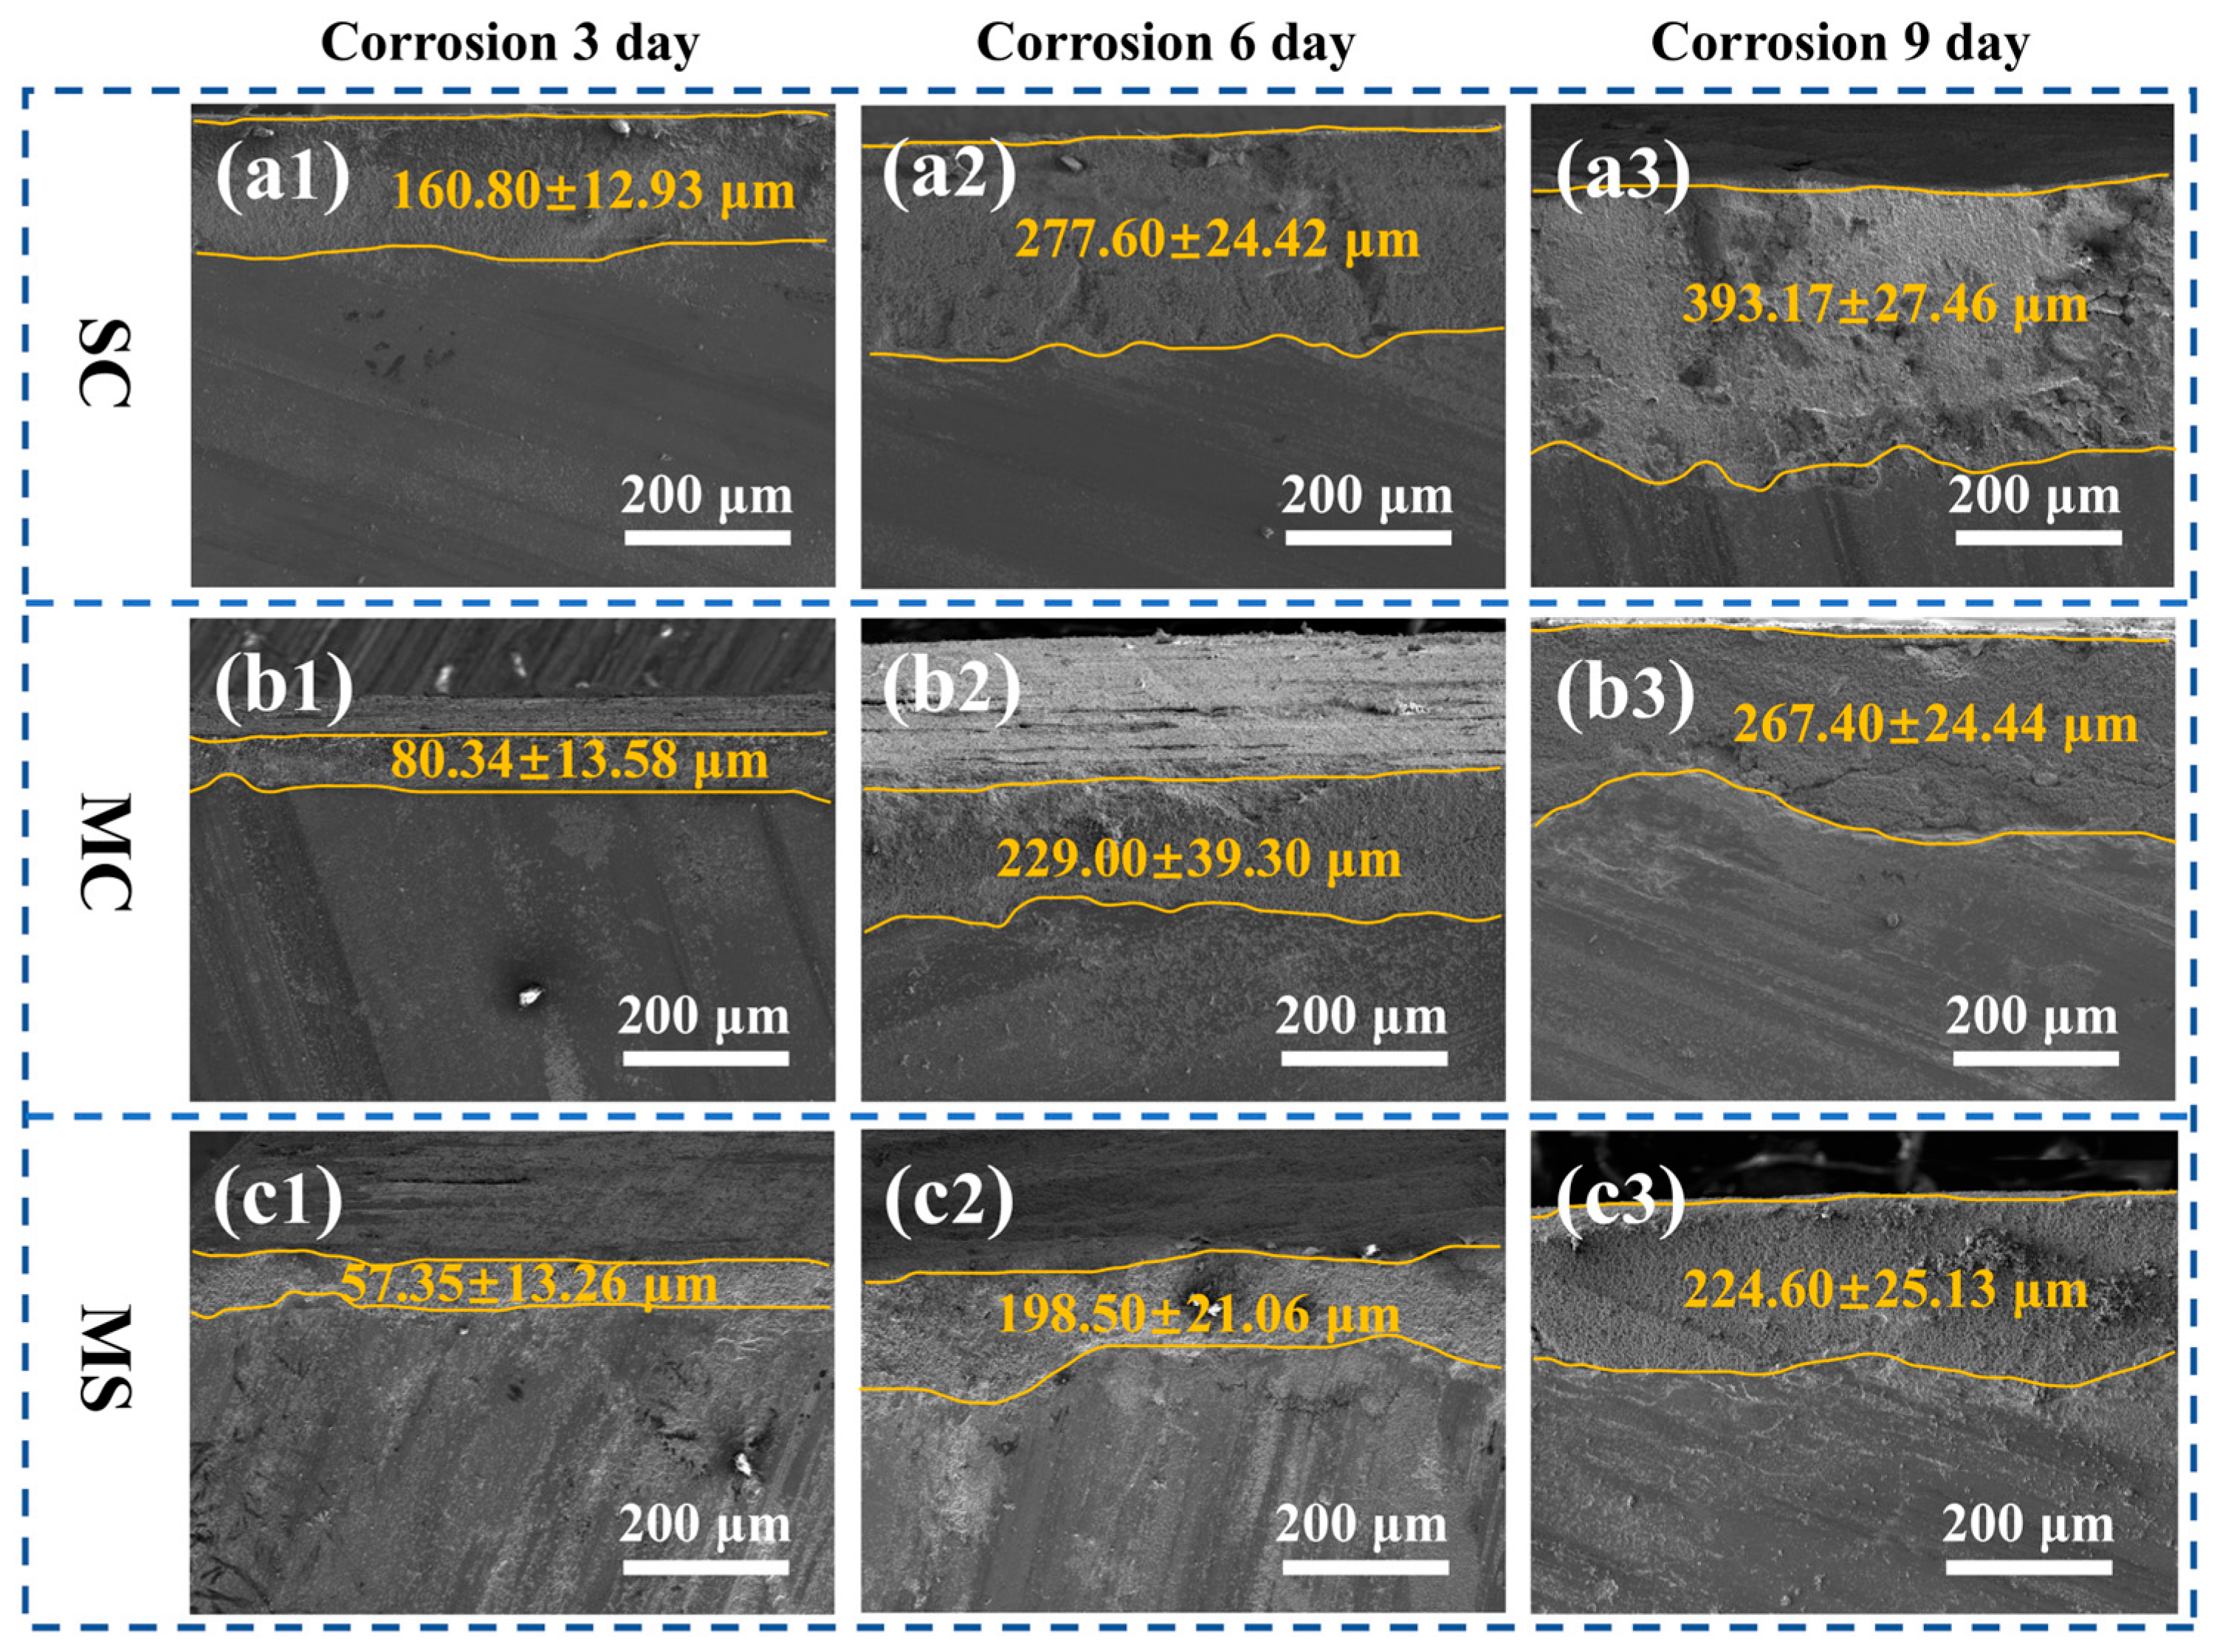
Cross-sectional morphologies of the samples after different corrosion durations were analyzed, and the corresponding SEM micrographs are shown in Figure 7. The microstructure can be divided into two distinct zones from top to bottom: a subsurface corrosion region characterized by a loose, porous structure, and an internal region exhibiting a relatively dense microstructure that remains largely unattacked.
As shown in Figure 7, the average corrosion depth (corresponding to the width of the porous subsurface region) of Samples SC, MC, and MS after 3, 6, and 9 days of hydrothermal corrosion is as follows: SC (160.80 ± 12.93, 277.60 ± 24.42, 393.17 ± 27.46 μm), MC (80.34 ± 13.58, 229.00 ± 39.30, 267.40 ± 24.44 μm), and MS (57.35 ± 13.26, 198.50 ± 21.06, 224.60 ± 25.13 μm). These results further confirm the hydrothermal corrosion resistance order: SC < MC < MS.
The XRD patterns of the corroded surfaces of reactive sintered SiC and SiC–MoSi2 samples after hydrothermal corrosion (345 °C, 15 MPa) for 9 days are shown in Figure 8. Only diffraction peaks corresponding to β-SiC and α-SiC are detected in all three samples. Compared to the pre-corrosion samples, the diffraction peaks of residual secondary phases, namely Si and MoSi2, have completely disappeared. It is reasonable to infer that these secondary phases were transformed into amorphous glassy phases (such as SiO2 and MoO3) during hydrothermal corrosion, which are not detectable by XRD [53]. Moreover, it is likely that a portion of these glassy phases dissolved into the aqueous medium, contributing to the observed weight loss.

3.4. Corrosion Mechanism and the Role of MoSi2

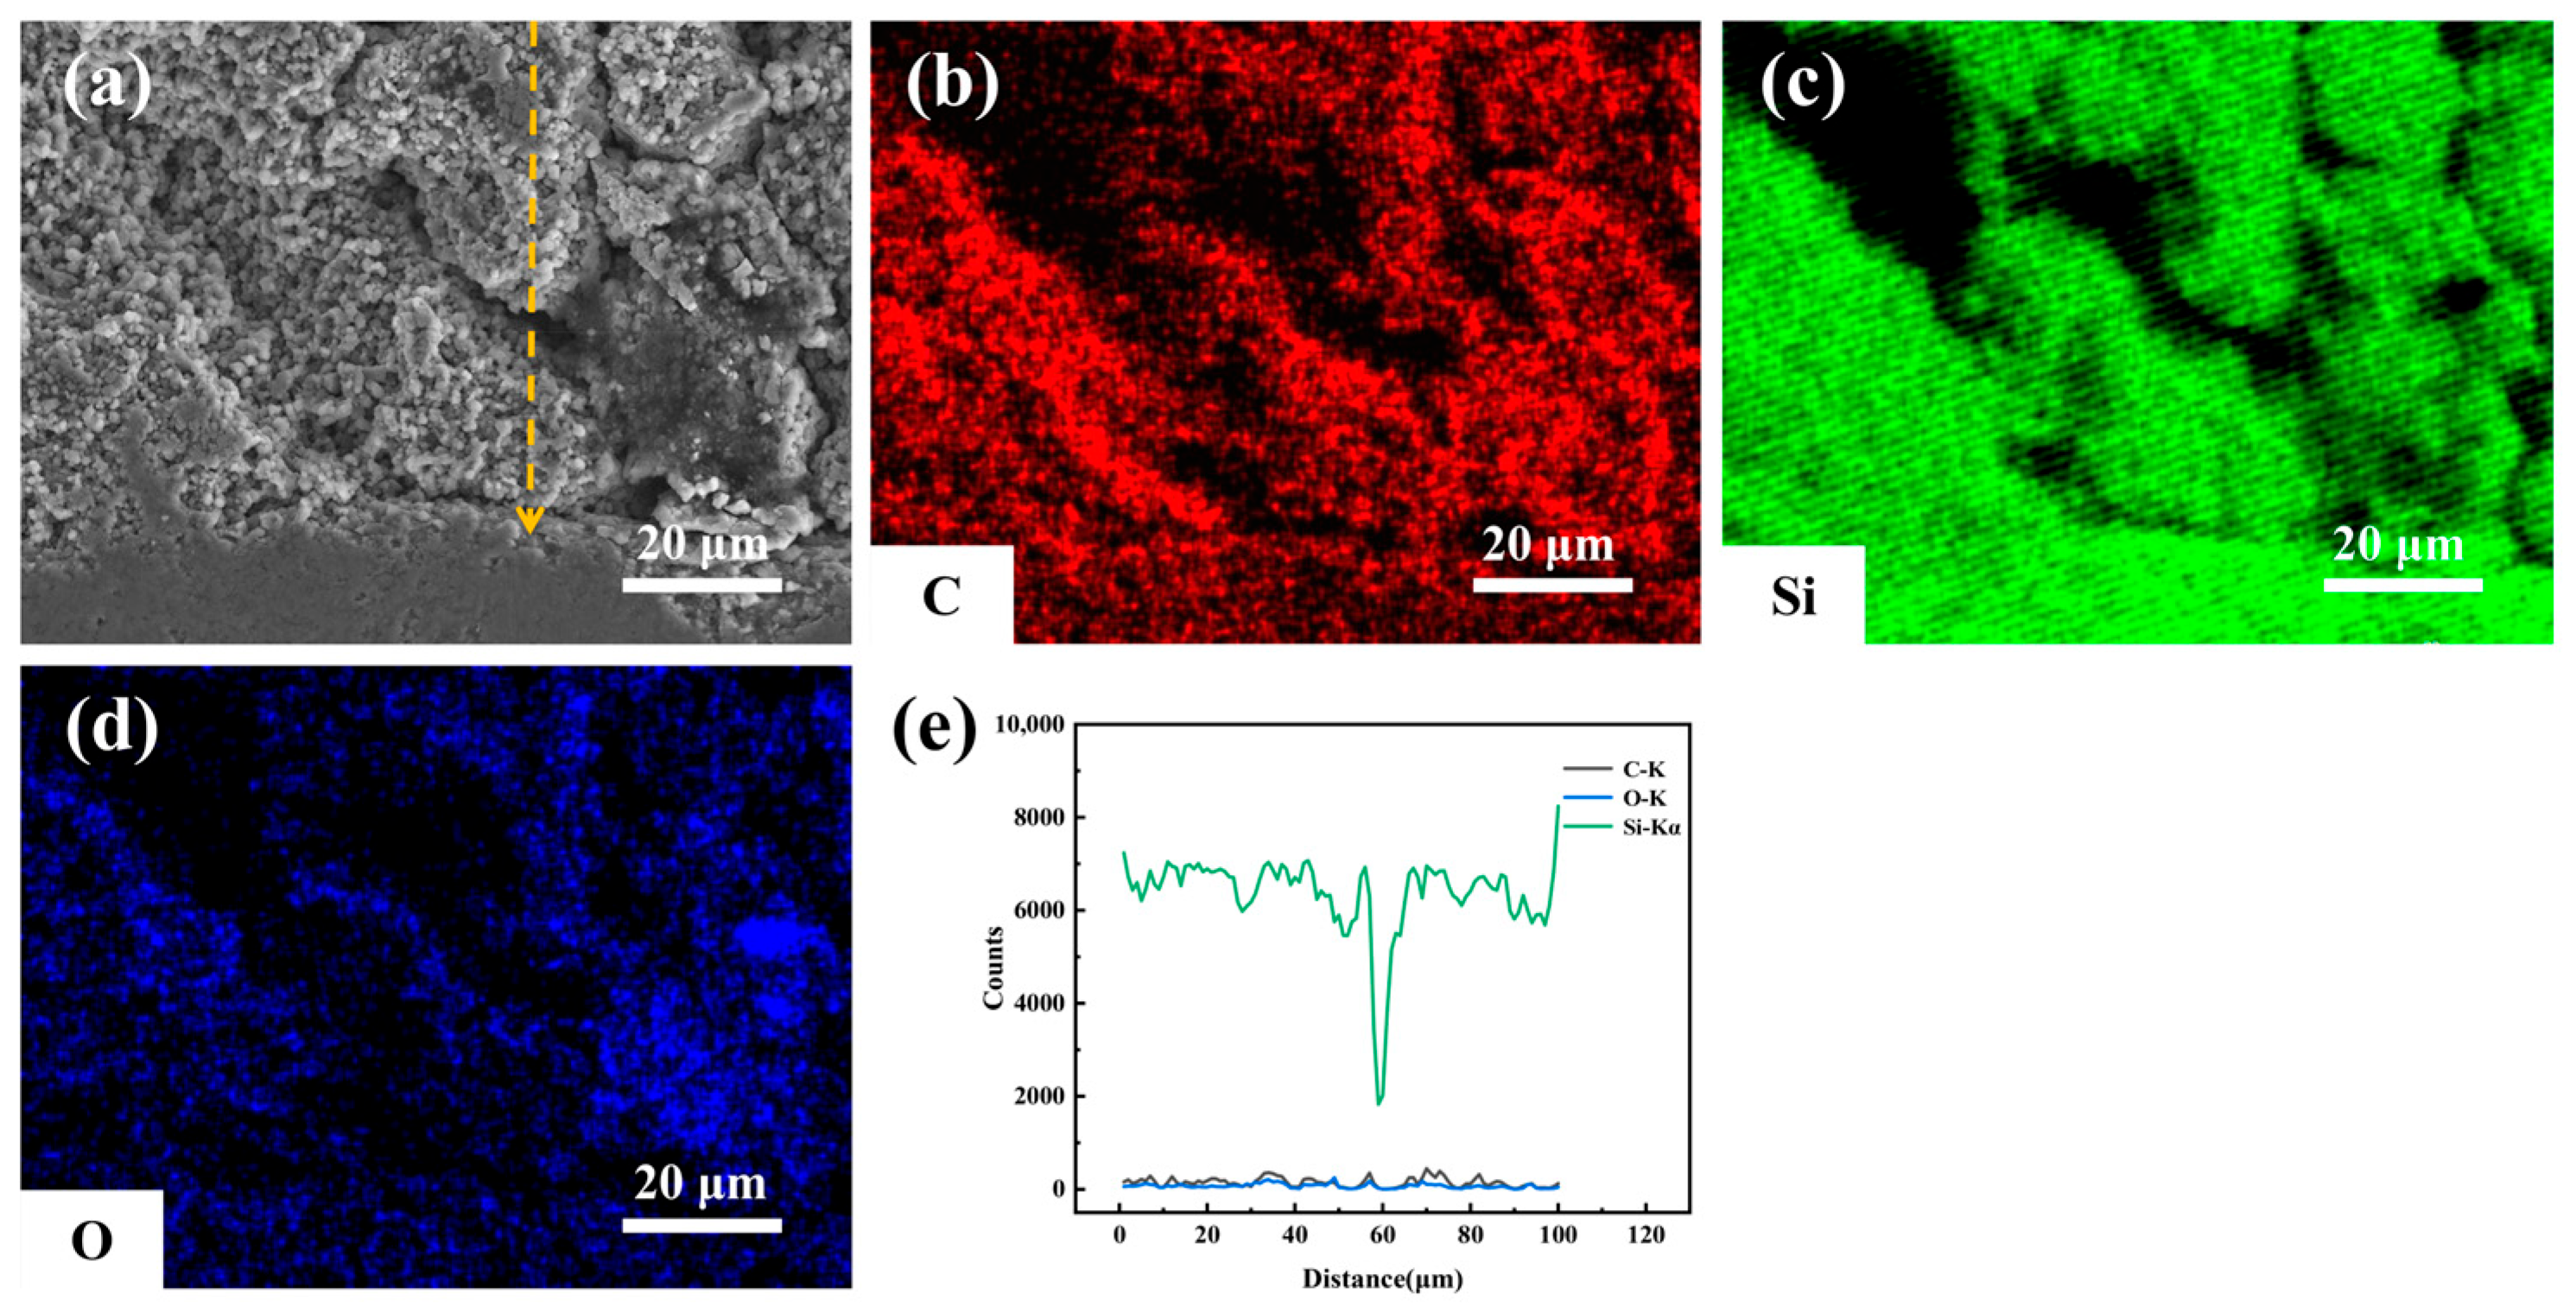
Figure 9 shows SEM-EDS analysis of the cross-sectional corrosion regions beneath the corroded surface of samples after 9 days of hydrothermal corrosion. Sample SC’s corrosion region exhibits obvious cracks and voids (some up to ~20 μm in diameter), consistent with its high weight loss (22.3970 ± 1.2059 mg/cm2). EDS elemental mapping reveals the corrosion region is mainly composed of Si, C, and O with highly coincident distributions, indicating it is predominantly SiC and SiO2. No distinct residual Si-enriched areas are detected, further confirming preferential dissolution and leaching of residual Si during corrosion. EDS line scans show a dominant Si signal across the entire cross-section (intrinsic to the SiC matrix), with line scan intensity representing relative counts rather than absolute atomic percentages.
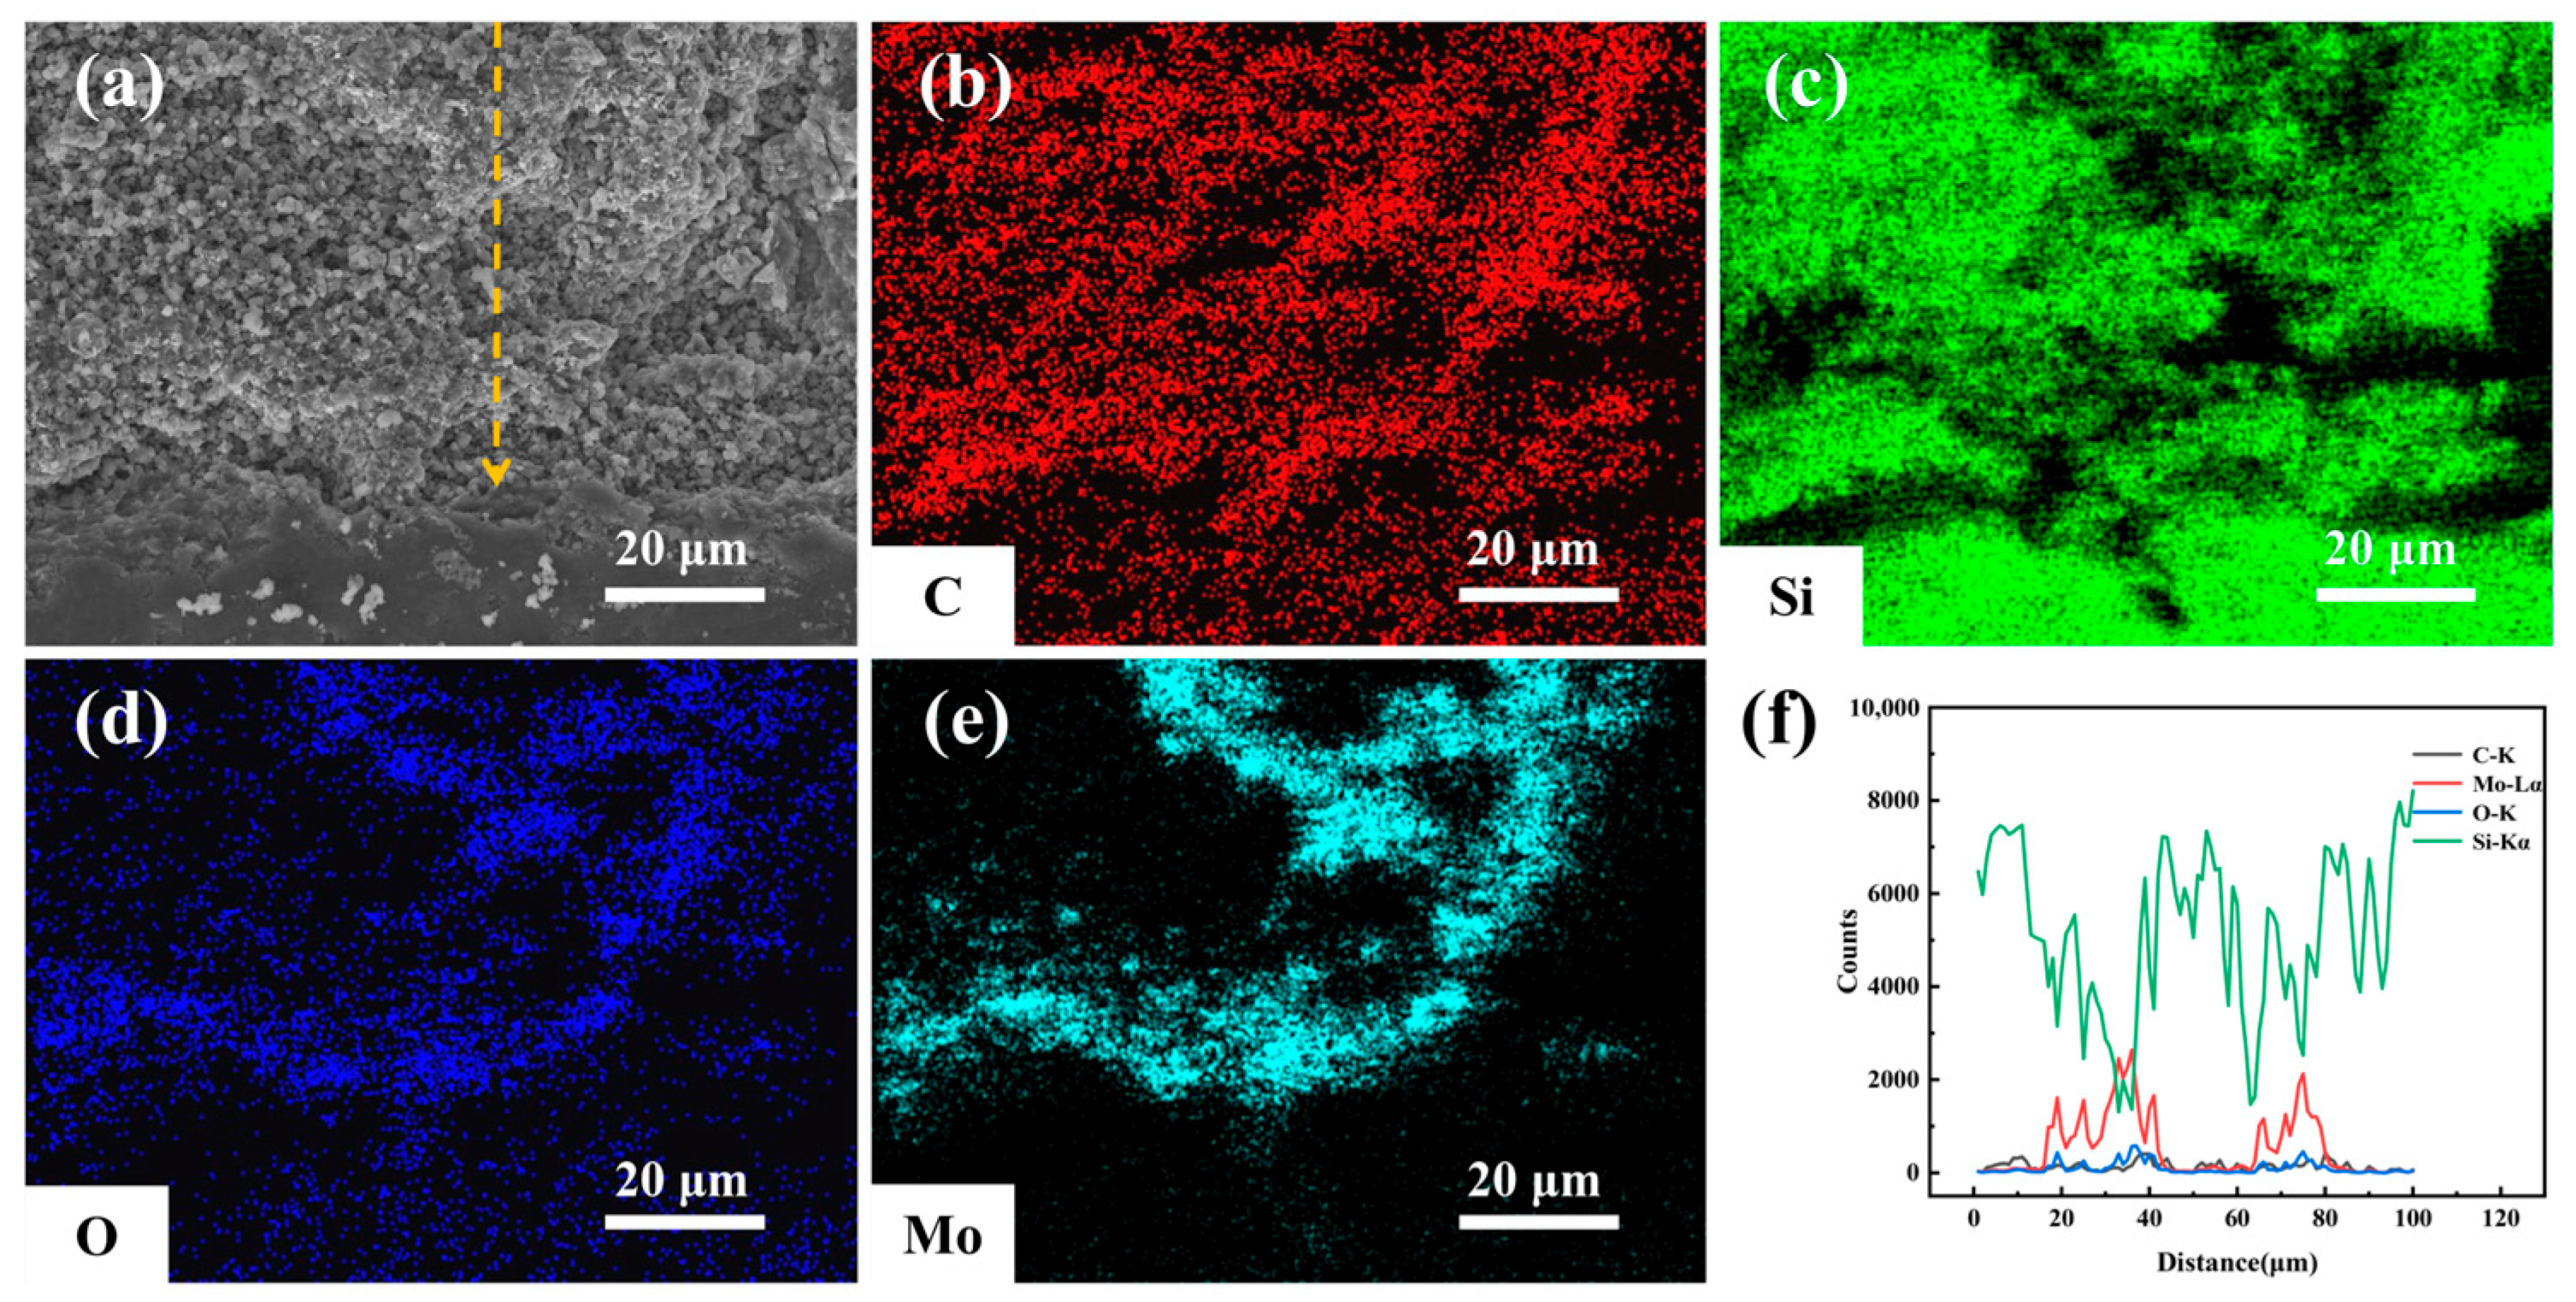
Figure 10 presents SEM-EDS characterization of the cross-sectional corrosion region directly beneath Sample MC’s corroded surface after 9 days of hydrothermal corrosion. While the corrosion region remains porous overall, it differs significantly from Sample SC, featuring fewer cracks, smaller pores, and a denser structure. EDS elemental mapping shows the corrosion region mainly contains Si, C, O, and Mo, indicating the presence of uncorroded SiC matrix and Mo- and Si-containing oxide phases. Notably, Mo is more concentrated in the corrosion region, suggesting the added MoSi2 exerts a positive effect on enhancing hydrothermal corrosion resistance. In the 20–40 μm and 60–80 μm corrosion layers, Mo and O signals exhibit co-enrichment peaks, while Si remains dominant across the cross-section, primarily due to the intrinsic signal of the SiC matrix.
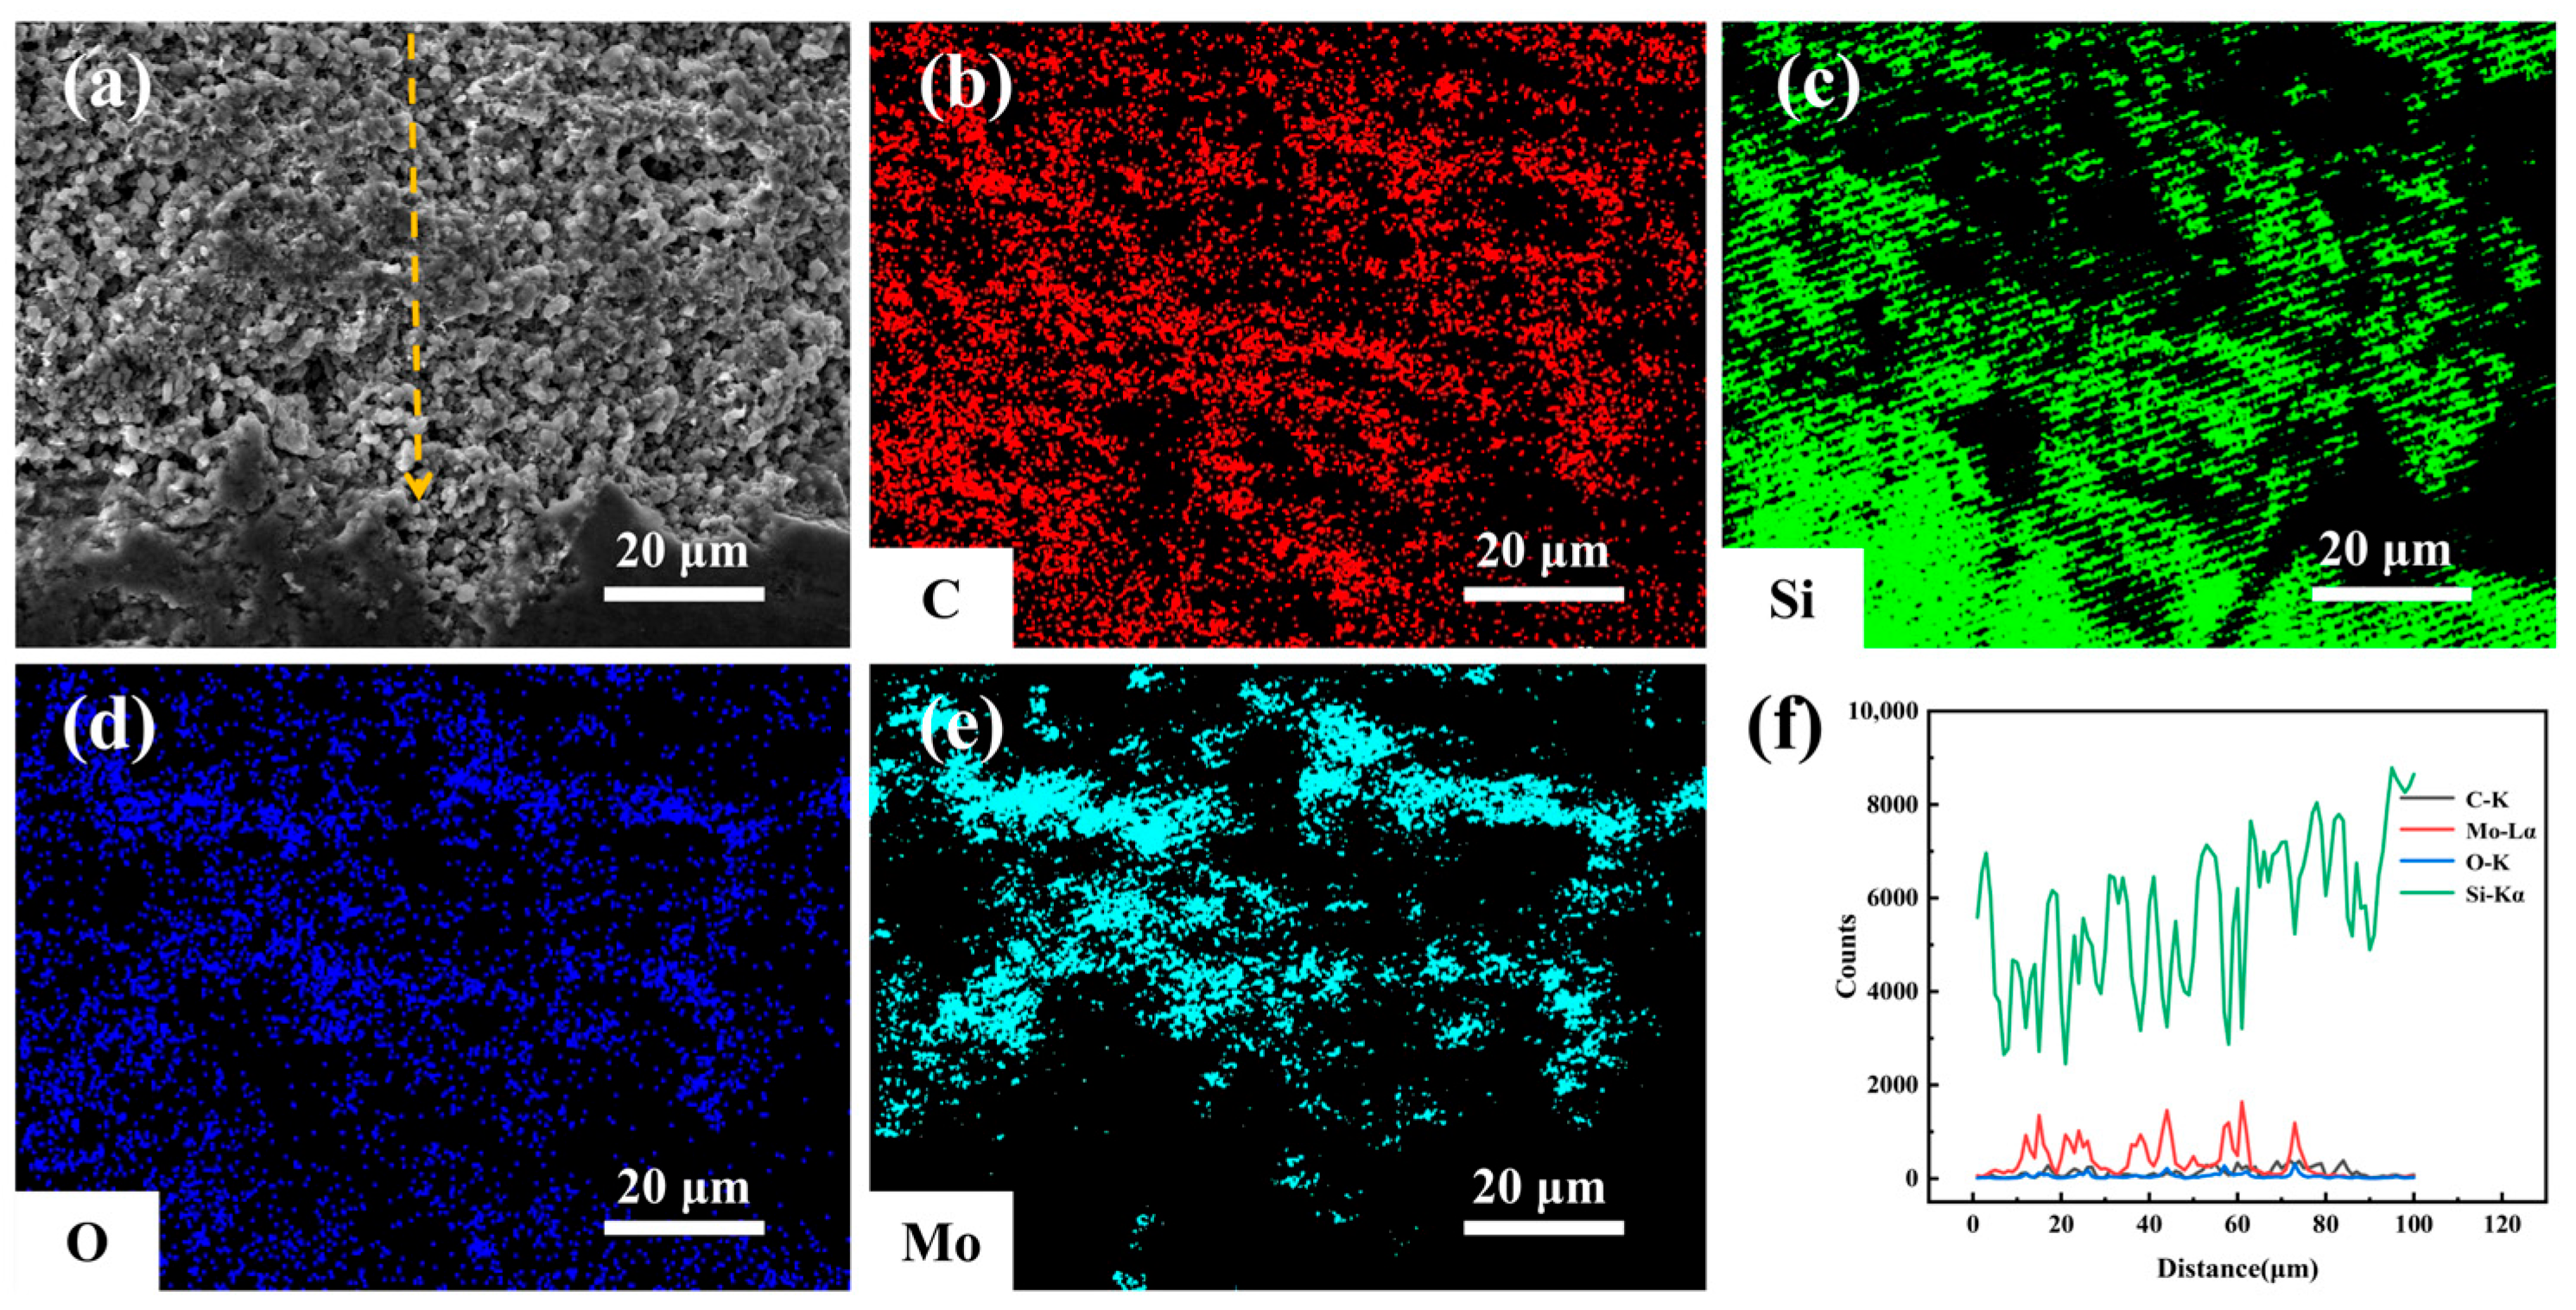
Figure 11 shows SEM-EDS characterization of the cross-sectional corrosion region directly beneath Sample MS’s corroded surface after 9 days of hydrothermal corrosion. Among the three samples, Sample MS’s corrosion region has the lowest porosity and a more homogeneous microstructure. EDS mapping reveals the presence of Si, C, O, and Mo, with notably uniform Mo distribution—likely the key to its denser corrosion layer. The uniform MoSi2 distribution in Sample MS further enhances its positive effect on hydrothermal corrosion resistance. EDS line scans show distinct co-enrichment peaks of Mo and O (synchronized distribution) in the 10–80 μm corrosion region, confirming the formation of a MoO3-SiO2 composite oxide layer. The dominant Si signal across the cross-section is attributed to the intrinsic SiC matrix.
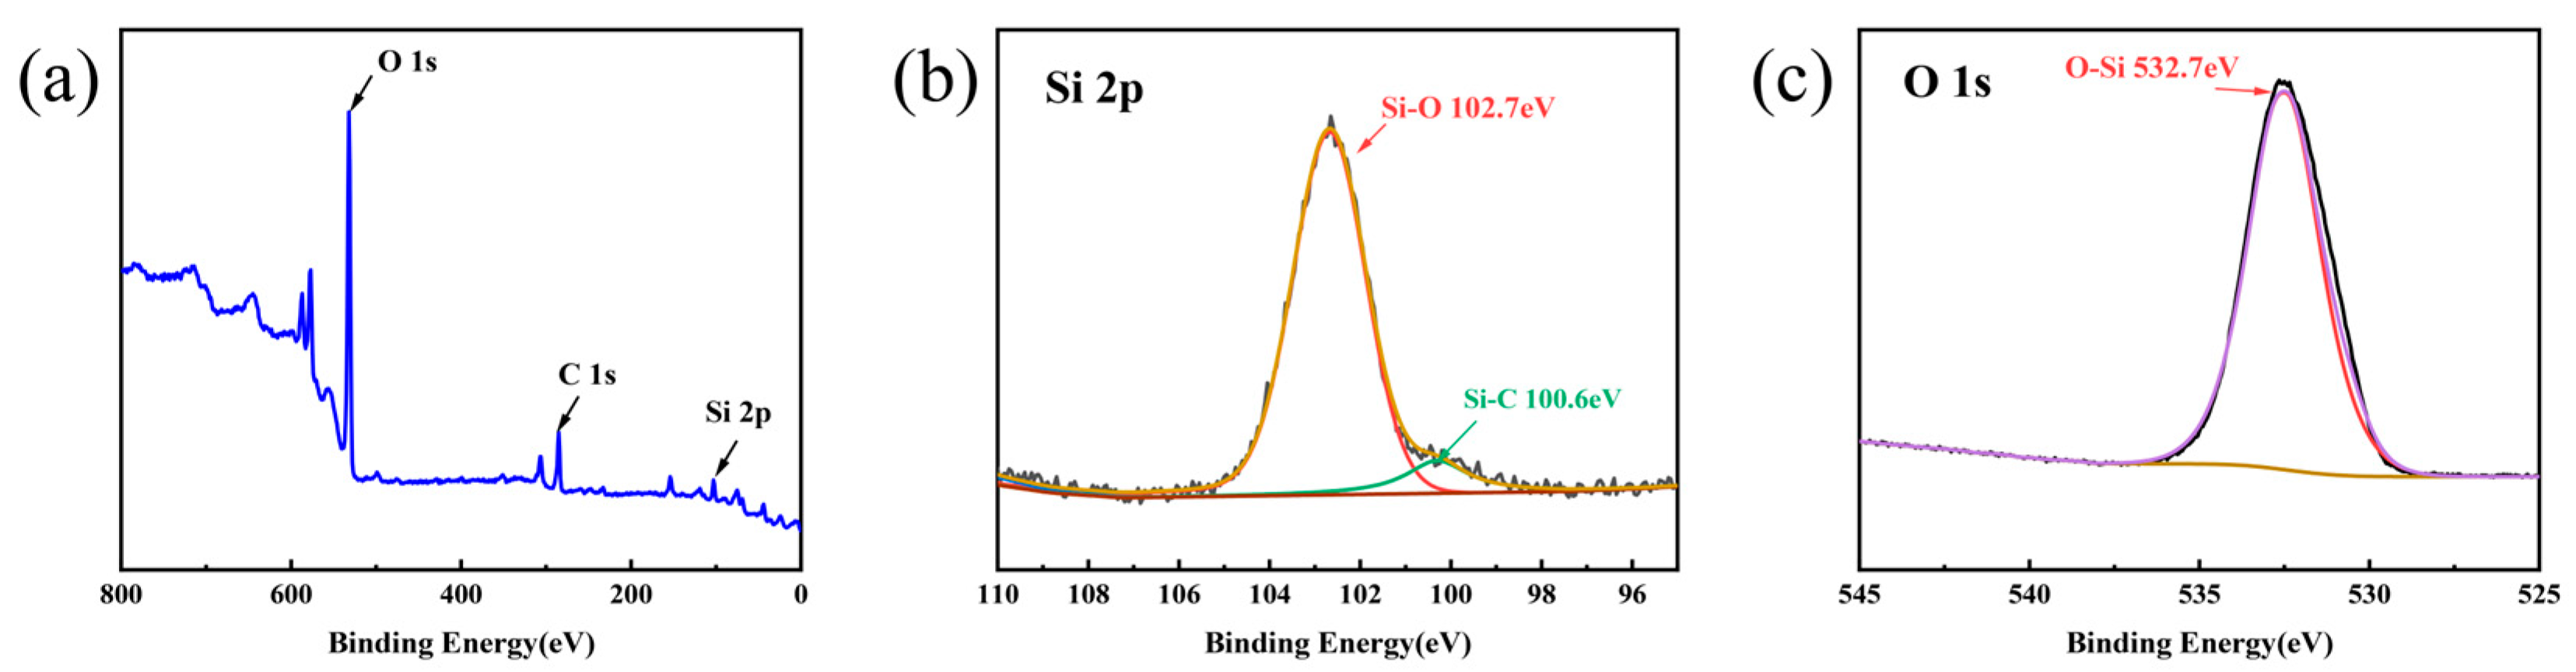
X-ray photoelectron spectroscopy (XPS) was used to characterize the surface elemental distribution and chemical bonding states of Sample SC after 9 days of hydrothermal corrosion (Figure 12). The survey spectrum shows the surface is mainly composed of O, C, and Si (Figure 12a). Fitting of the high-resolution Si 2p spectrum identifies Si–O (102.7 eV) and Si–C (100.6 eV) bonds (Figure 12b) [54], while O 1s spectrum fitting confirms O–Si bonds (532.7 eV) (Figure 12c) [55,56], confirming SiO2 and SiC on the corroded surface. The absence of Si–Si bonds in the Si 2p spectrum indicates complete corrosion of the surface residual silicon.
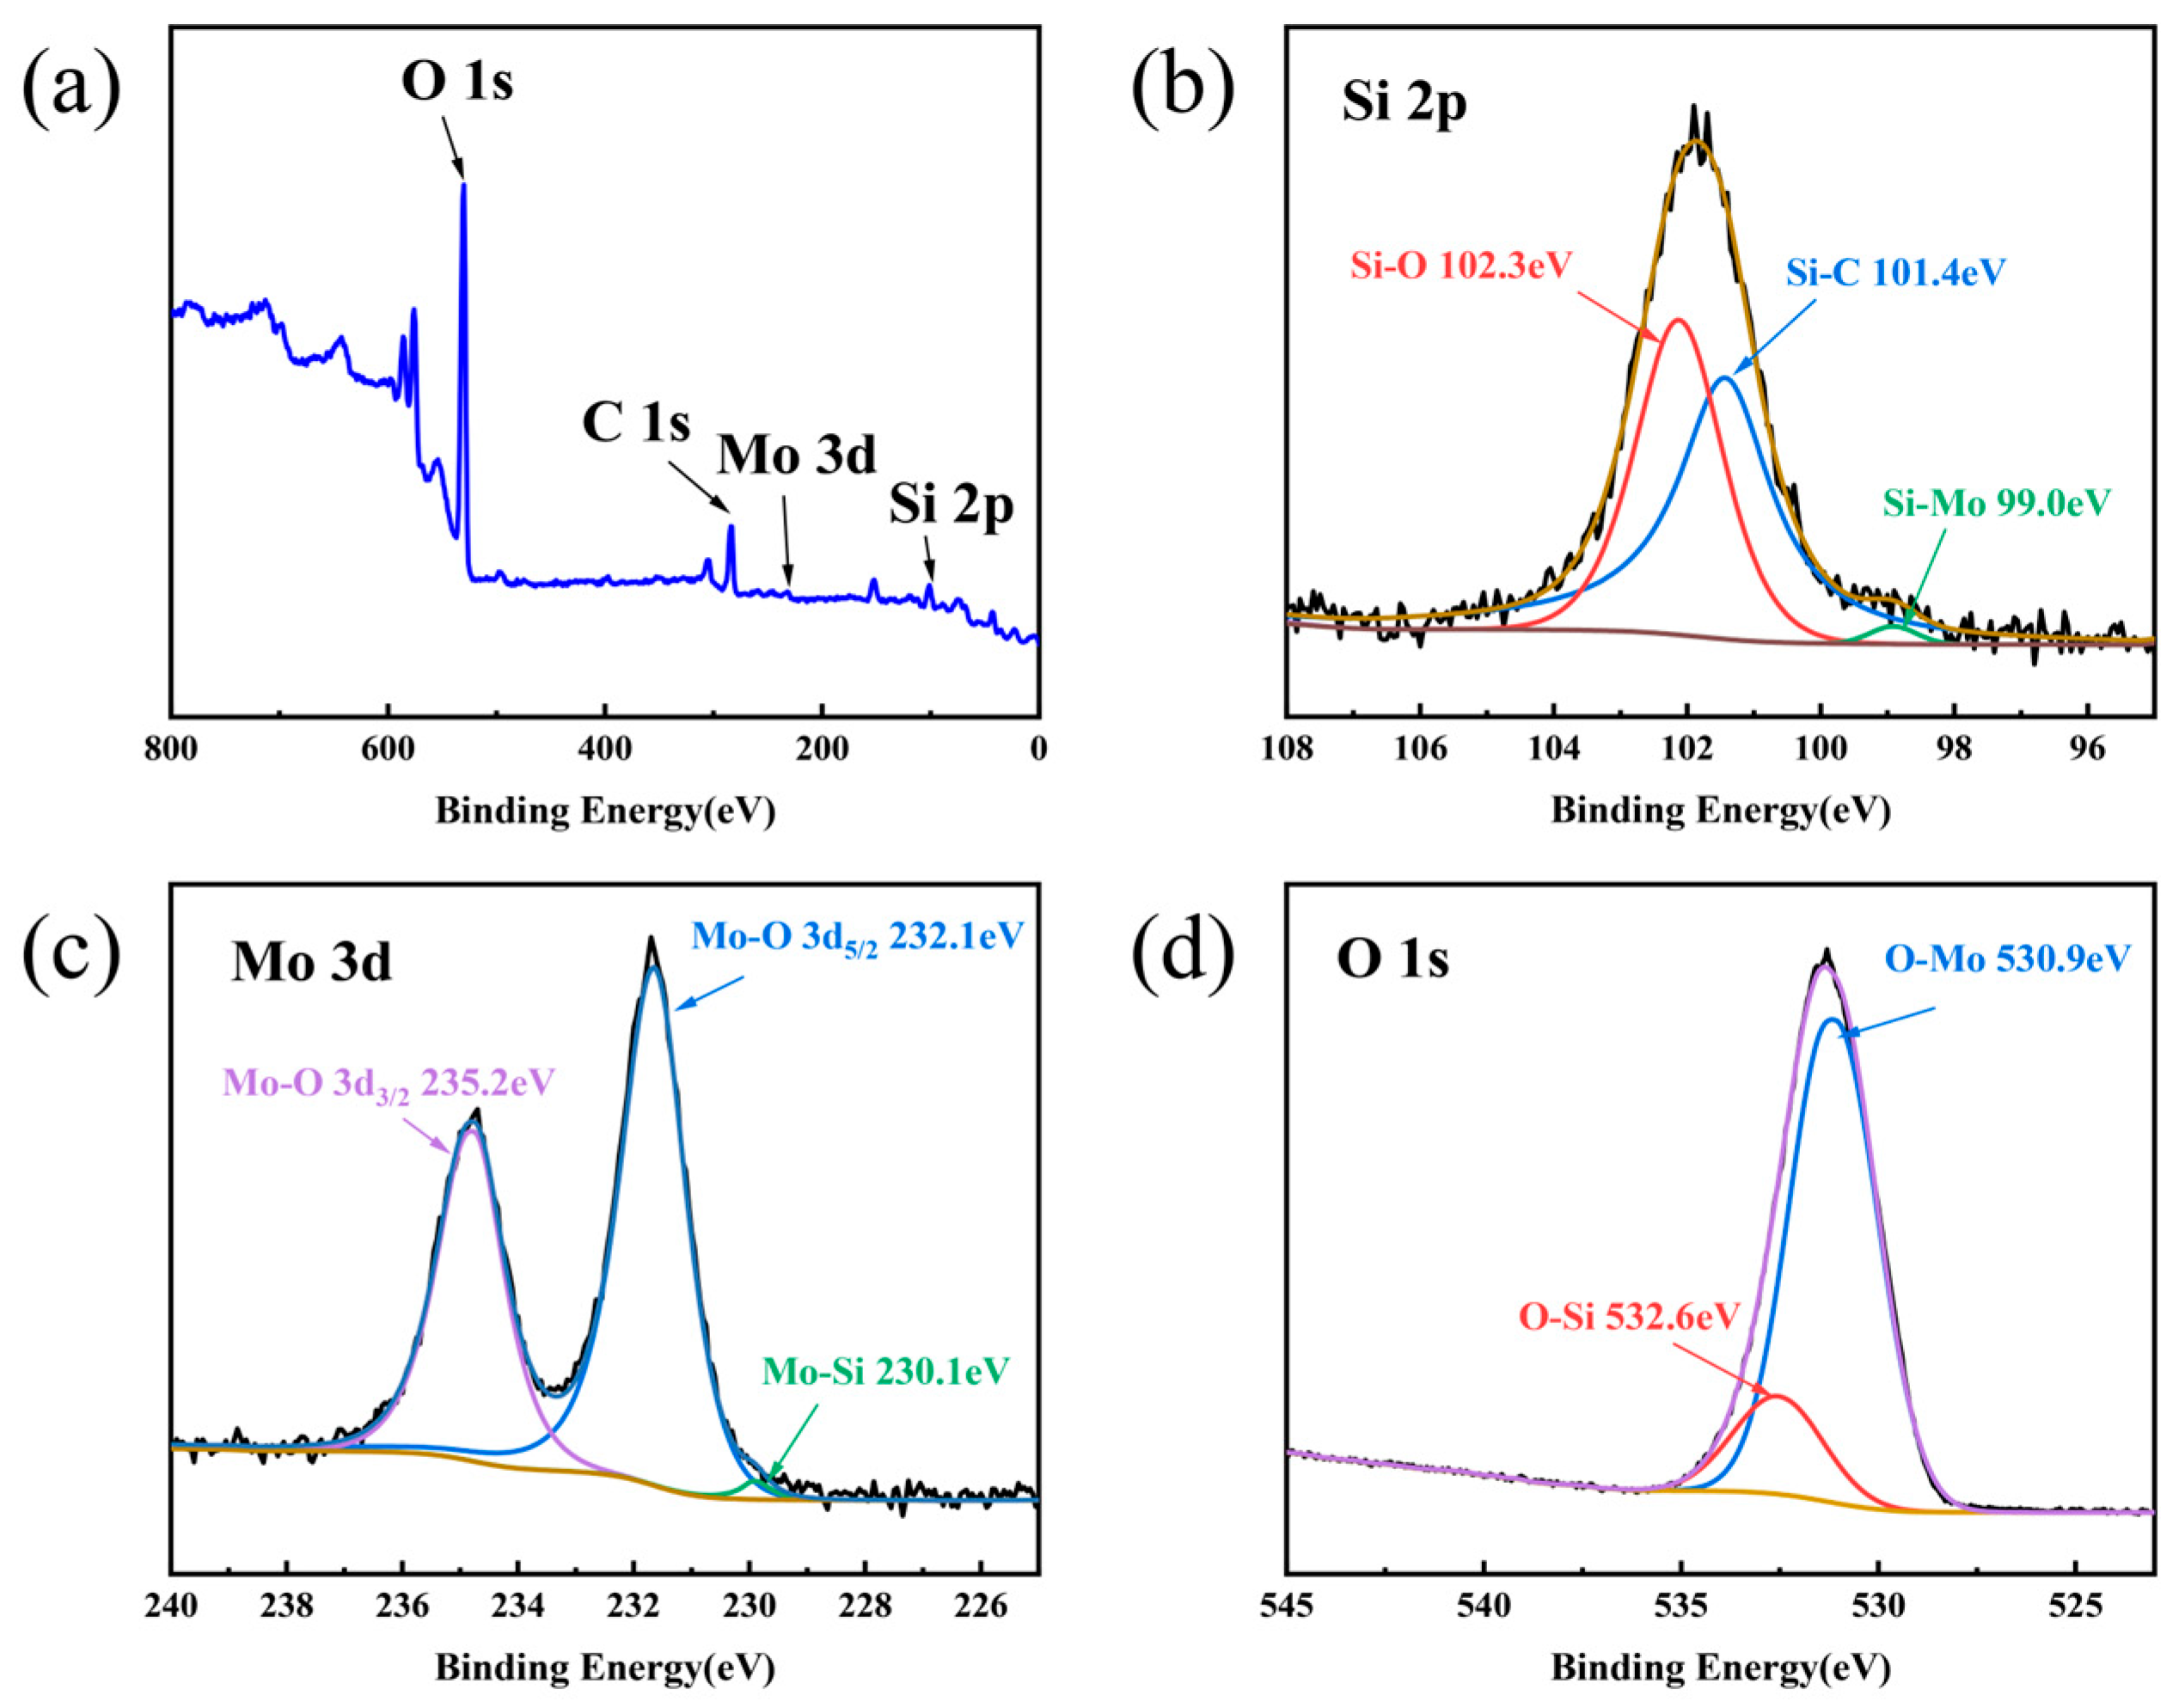
To investigate the corrosion behavior of the MC sample in a 345 °C, 15 MPa hydrothermal environment, XPS was used to analyze the surface elemental composition and chemical bonding states after 9 days of corrosion. Figure 13 shows the XPS survey spectrum and the high-resolution spectra of Si 2p, Mo 3d, and O 1s for the corroded surface. After 9 days of hydrothermal corrosion, the surface of MC-6 is mainly composed of O, C, Mo, and Si (Figure 13a). In Figure 13b, peak fitting of the high-resolution Si 2p spectrum reveals three components: Si–O bonds (102.3 eV), Si–C bonds (101.4 eV), and Si–Mo bonds (99.0 eV). In Figure 13c, peak fitting of the high-resolution Mo 3d spectrum identifies three characteristic peaks corresponding to Mo–O (3d3/2) bonds (235.2 eV), Mo–O (3d5/2) bonds (232.1 eV), and Mo–Si bonds (230.1 eV). In Figure 13d, the high-resolution O 1s spectrum is fitted into O–Si bonds and O–Mo bonds with binding energies of 532.6 eV and 530.5 eV, respectively [57,58,59,60,61]. Based on the above results, the presence of SiC, MoSi2, SiO2, and MoO3 can be confirmed on the corroded surface of the MC sample. Meanwhile, no Si–Si bonds are detected in the high-resolution Si 2p spectrum, indicating that the residual silicon on the sample surface has been completely corroded.
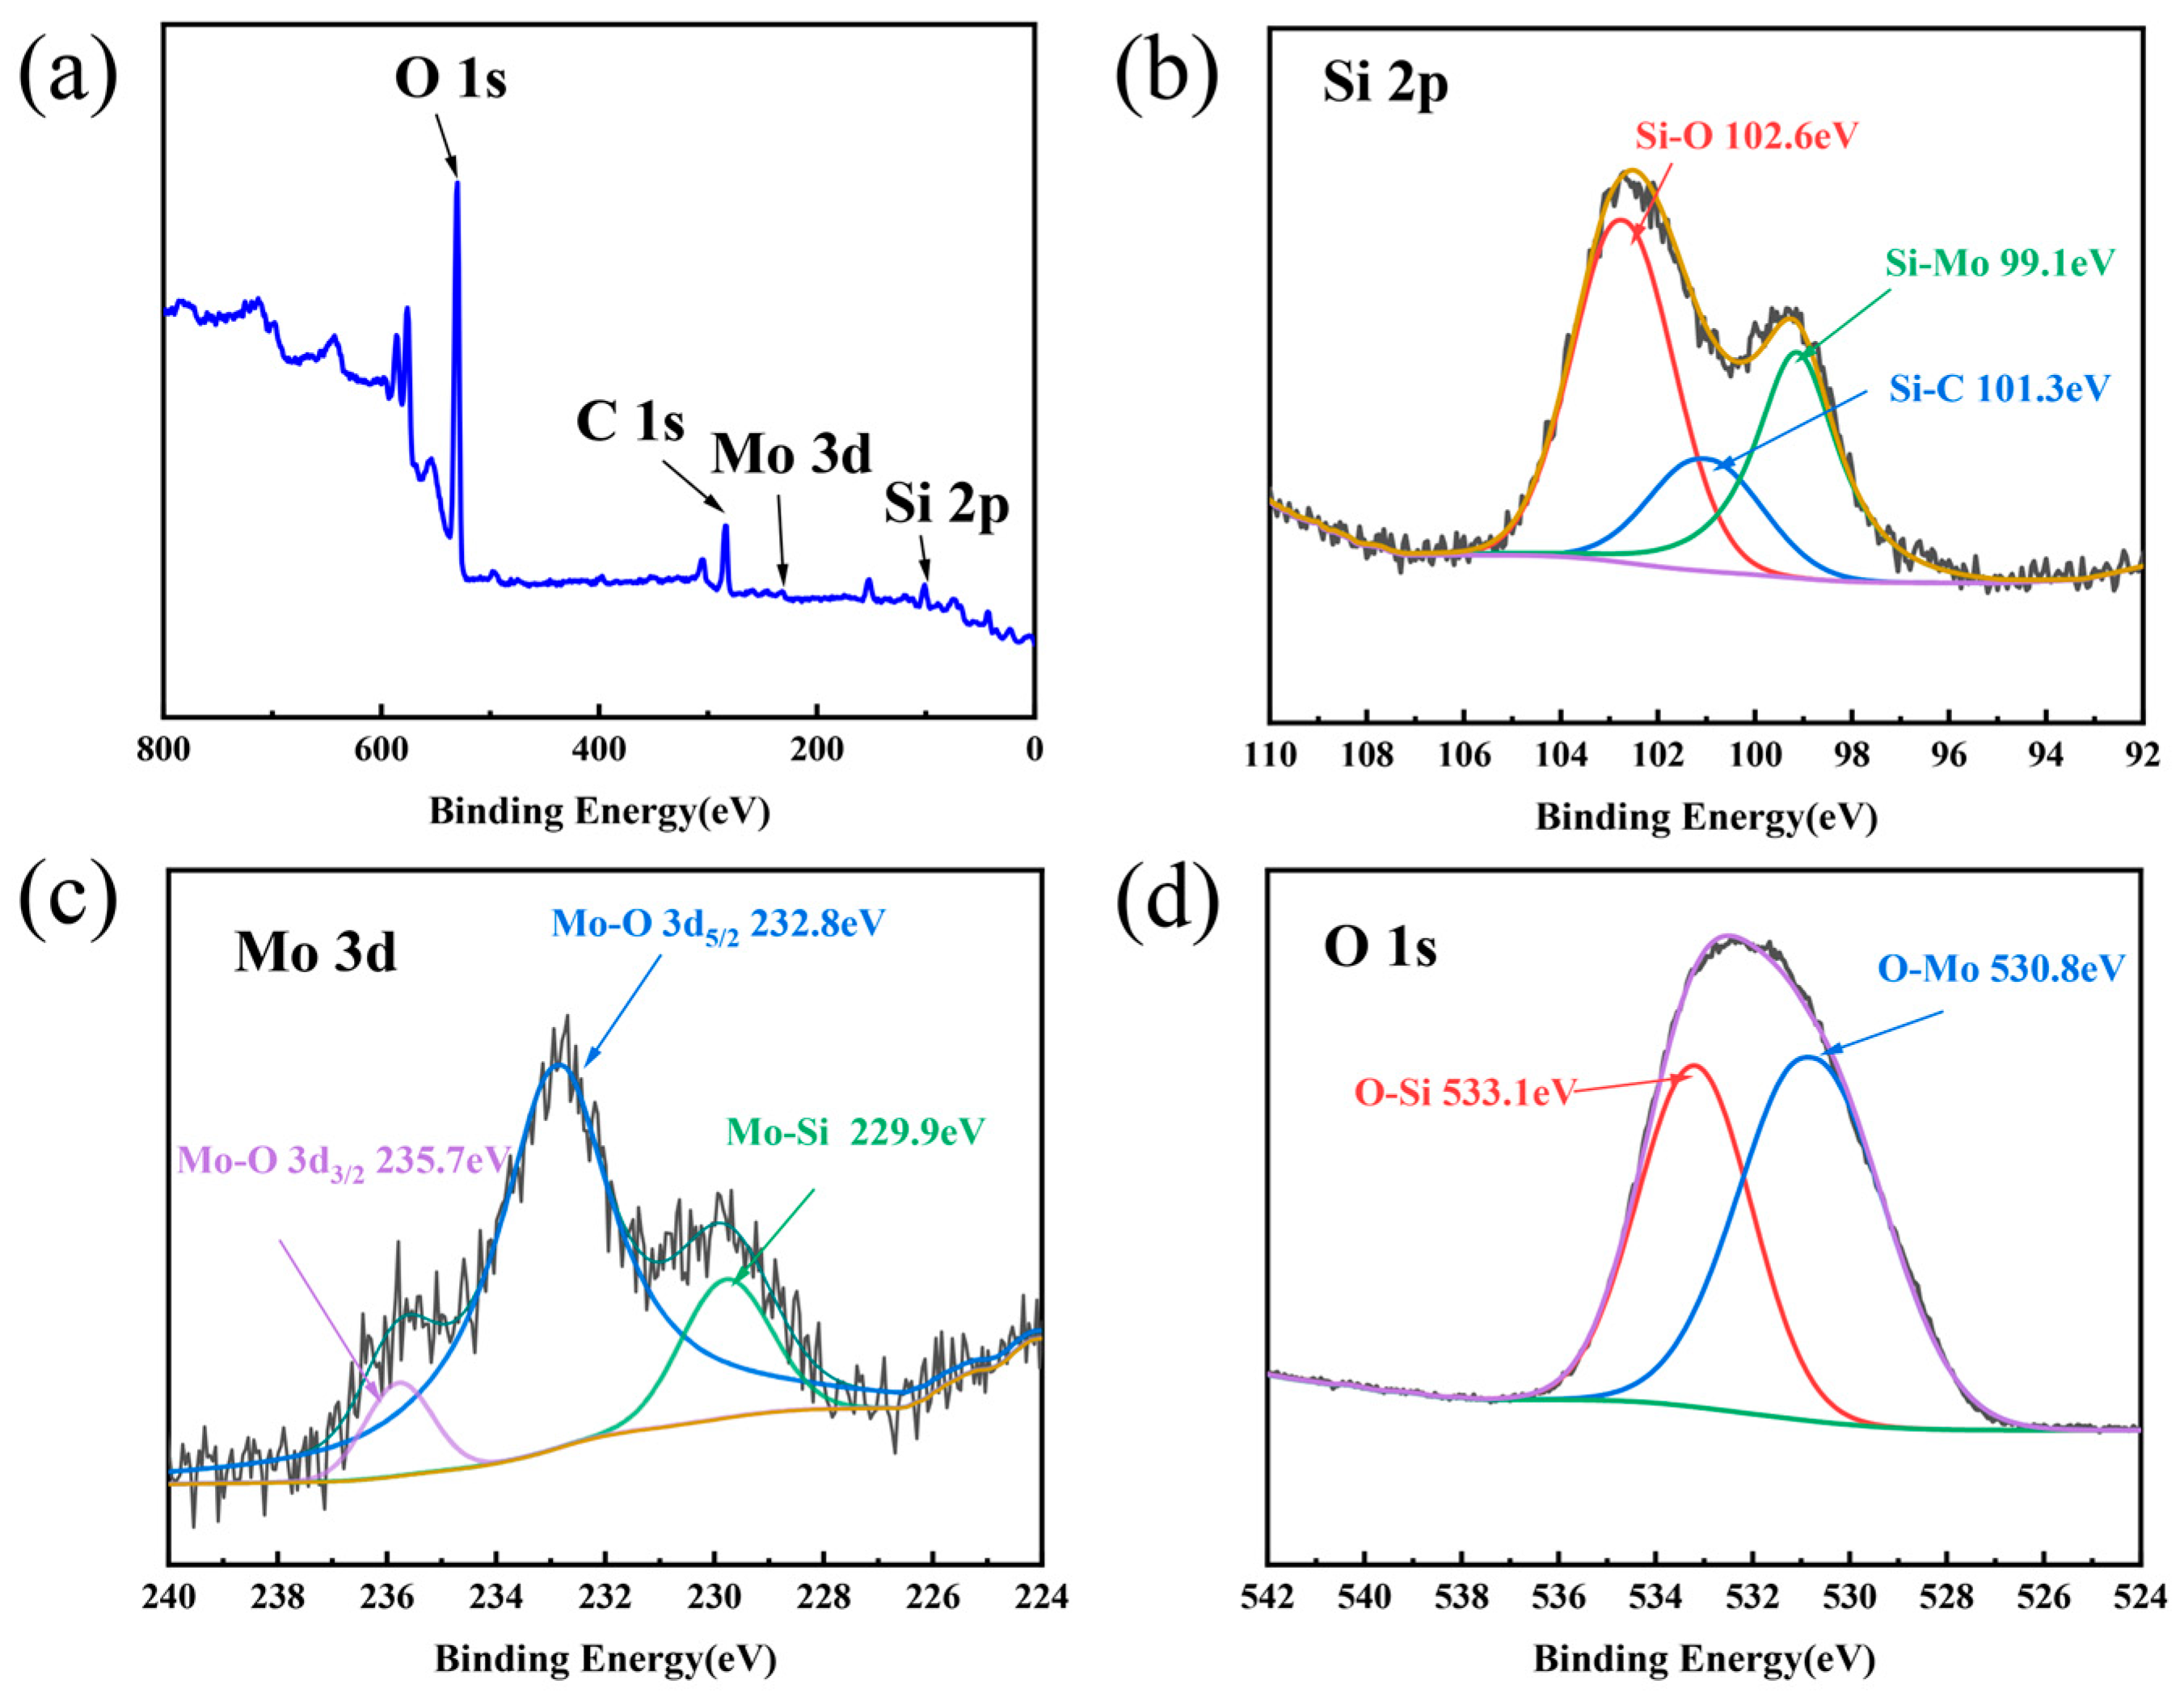
XPS was employed to reveal the elemental composition and chemical states on the surface of Sample MS after 9 days of hydrothermal corrosion. The survey scan spectrum (Figure 14a) displays characteristic peaks corresponding to Si 2p, Mo 3d, C 1s, and O 1s. The high-resolution Si 2p spectrum (Figure 14b) was deconvoluted into three peaks at binding energies of 99.1 eV, 101.3 eV, and 102.6 eV, assigned to Si–Mo, Si–C, and Si–O bonds, respectively. The high-resolution Mo 3d spectrum (Figure 14c) also comprises three peaks at 229.9 eV, 232.8 eV, and 235.7 eV, corresponding to Mo–Si, Mo–O (3d3/2), and Mo–O (3d5/2) bonds, respectively. The high-resolution O 1s spectrum (Figure 14d) is composed of two peaks at 530.8 eV and 533.1 eV, attributed to O–Mo and O–Si bonds, respectively. These results suggest that the corroded surface of Sample MS contains SiC, MoSi2, SiO2, and MoO3 [62,63,64,65,66]. Furthermore, the absence of a characteristic peak corresponding to Si–Si bonds indicates that no elemental silicon remains on the corroded surface.
Based on the above results, the three samples (SC, MC, and MS) exhibit distinctly different hydrothermal corrosion resistances, which are closely related to their composition and microstructure. Analysis of the residual phases in the corroded regions leads to the reasonable inference that the intrinsic hydrothermal corrosion resistance of the constituent phases follows the order Si < MoSi2 < SiC. During hydrothermal corrosion, the Si, MoSi2, and SiC constituents in the reactive sintered samples are likely oxidized via the following reactions [26,67,68]:
Si(s) + 2H2O(l) = SiO2(s) + 2H2(g)
MoSi2(s) + 7H2O(l) = MoO3(s) + 2SiO2(s) + 7H2(g)
SiC(s) + 3H2O(l) = SiO2(s) + CO(g) + 3H2(g)
Subsequently, the SiO2 product may undergo further hydrothermal corrosion via the following reactions [69]:
SiO2(s) + H2O(l) = H2SiO3(aq)
SiO2(s) + 2H2O(l) = Si(OH)4(aq)
The products H2SiO3 and Si(OH)4 dissolve in water, forming weakly acidic solutions that can undergo ionization, rendering the corroded sample surface porous and loose.
As evident from the above chemical equations, residual silicon is ultimately completely consumed by hydrothermal corrosion, with its products (H2SiO3 and Si(OH)4) dissolving in the aqueous medium, thereby creating pores within the corrosion region. This allows the ingress of high-temperature, high-pressure water further into the sample, continuing the corrosion process. In contrast, MoSi2 is oxidized to MoO3, which has extremely low solubility in high-temperature and high-pressure aqueous environments and can stably remain in the corrosion layer [69,70]. The low-solubility MoO3 exerts a pinning effect on soluble SiO2, immobilizing it in the oxide film and suppressing its excessive dissolution and loss. This maintains a relatively dense microstructure, protecting the underlying uncorroded matrix from further hydrothermal corrosion. Thus, Mo significantly improves the compactness and structural stability of the MoO3-SiO2 composite oxide layer, inhibits its further dissolution into highly soluble H2SiO3 and Si(OH)4, and ultimately enhances the material’s hydrothermal corrosion resistance.
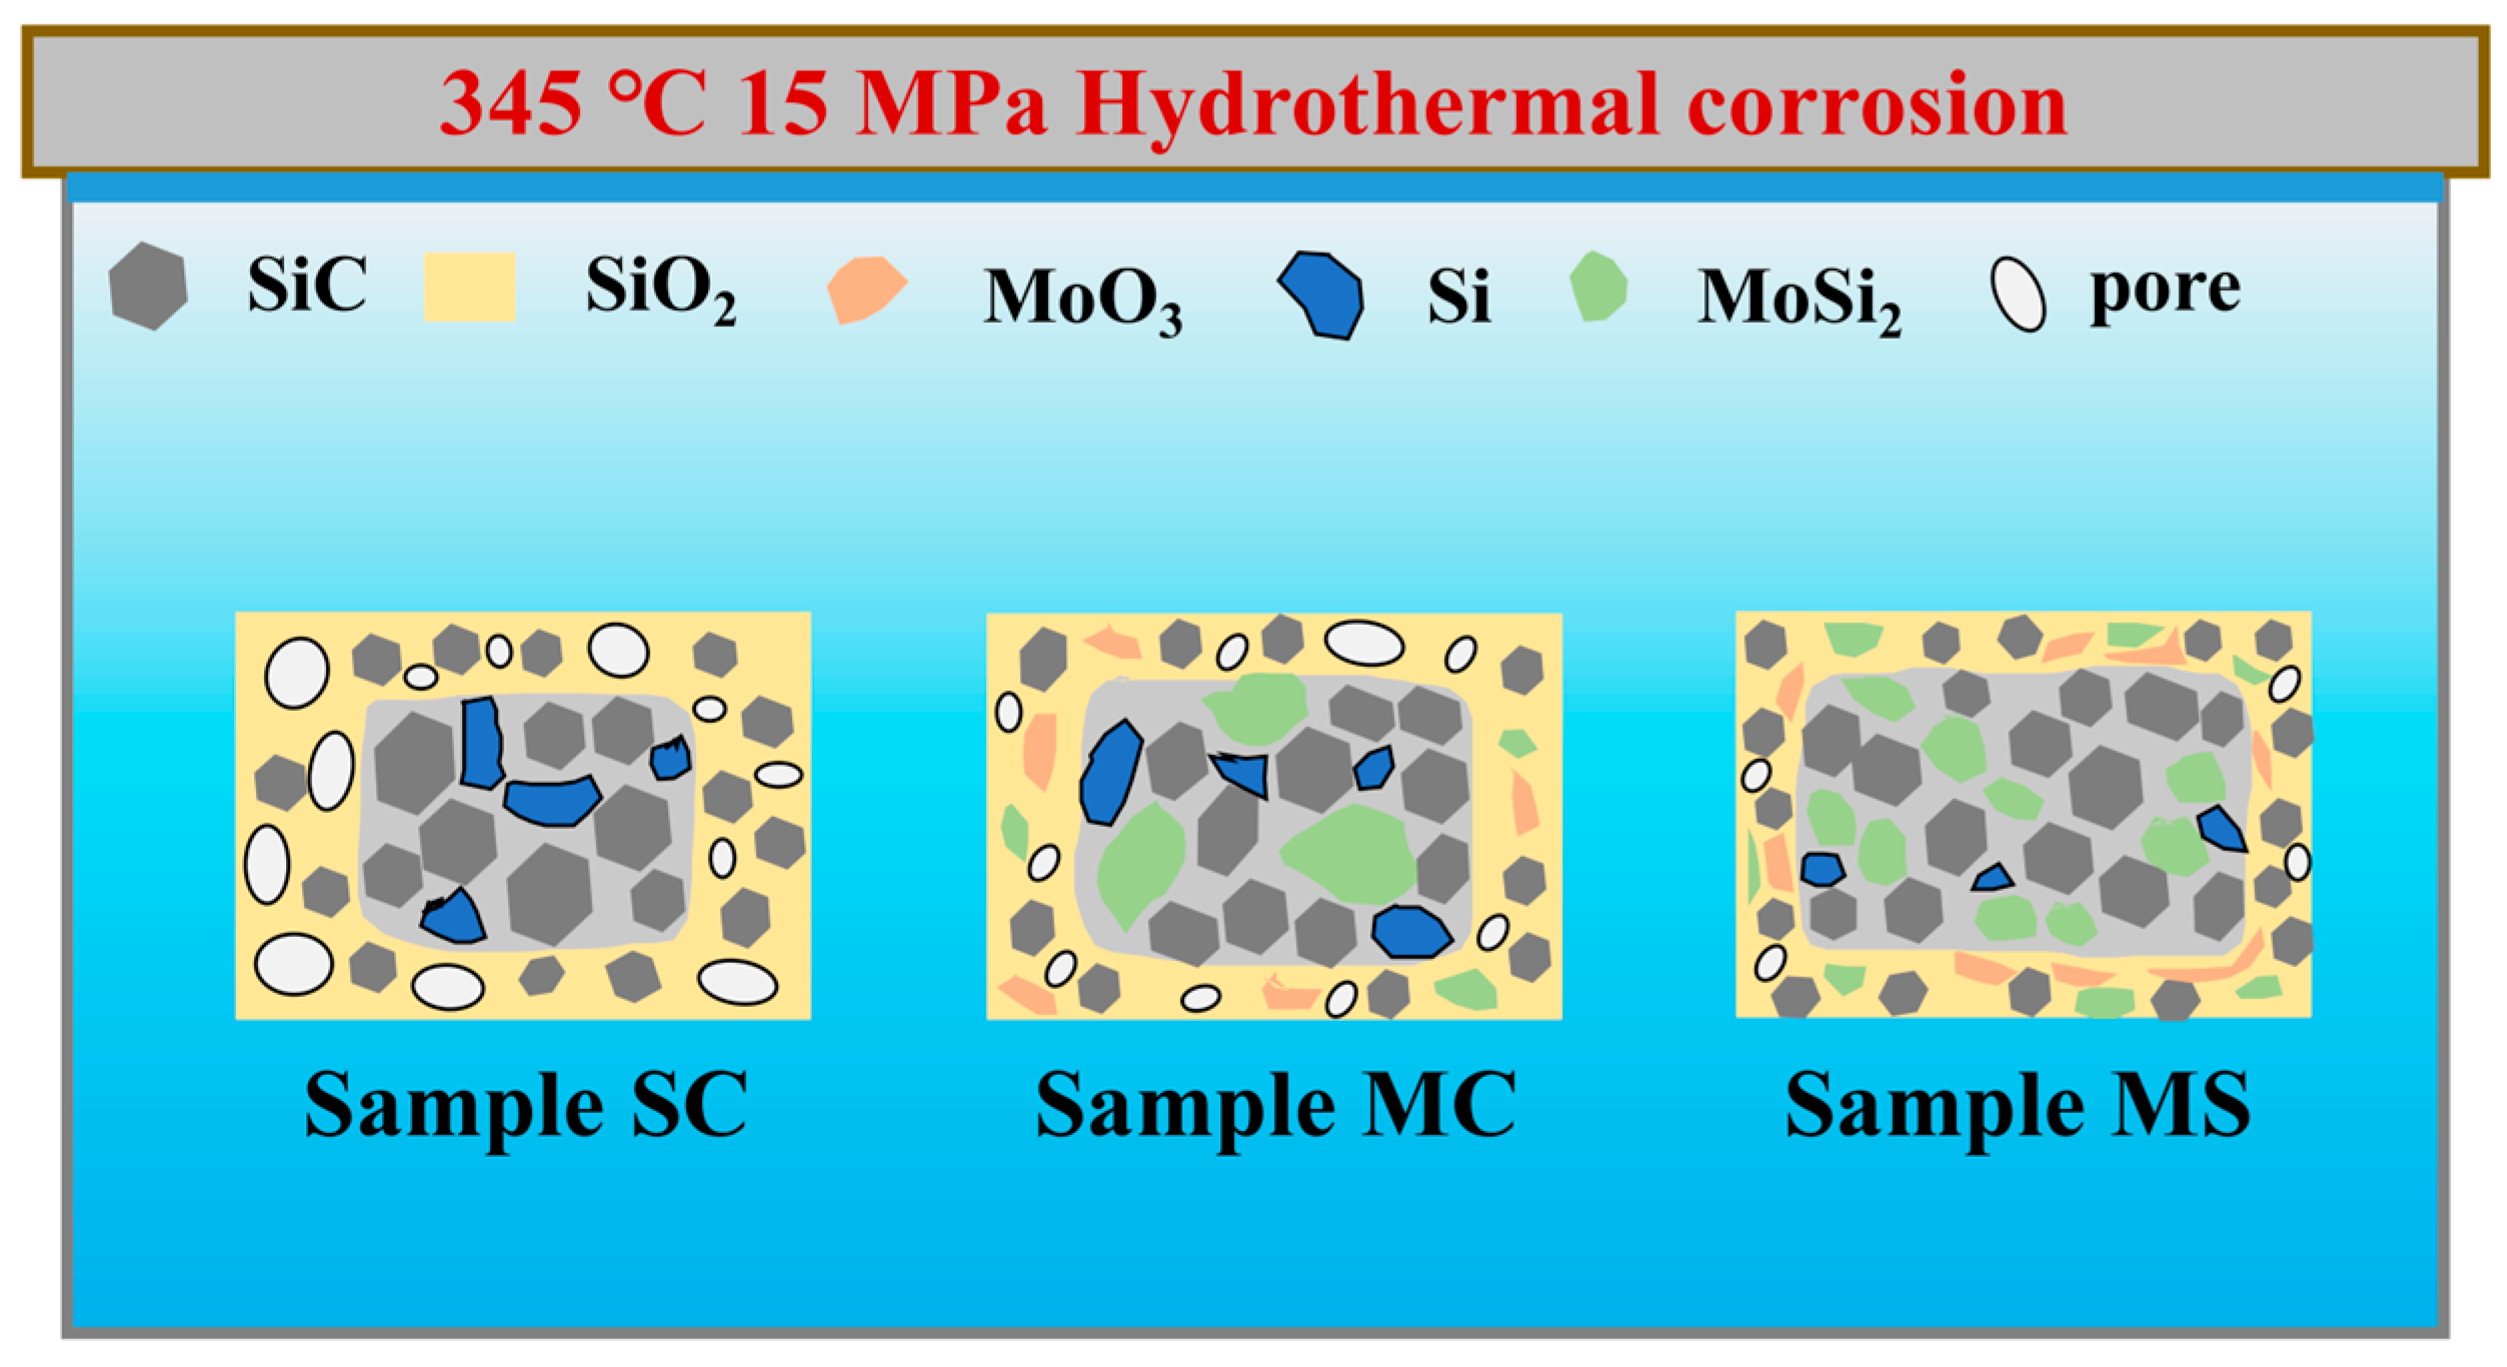
A comparison of the hydrothermal corrosion mechanisms of the three samples is schematically illustrated in Figure 15. From a microstructural perspective, the SC sample is characterized by a high (19.17 ± 1.01 vol.%) and continuously distributed residual silicon phase. During the initial stage of hydrothermal corrosion, its surface is corroded, forming through-penetrating macropores. As corrosion proceeds, a dynamic cycle of “continuous reaction–pore expansion” is established, ultimately resulting in the highest weight loss and deepest corrosion depth.
For Sample MC, the residual silicon content is reduced to 12.43 ± 0.86 vol.%, and MoSi2 is present as a secondary phase. However, its microstructure is insufficiently uniform: the presence of large residual Si blocks and unevenly distributed MoSi2 still limits the improvement in corrosion resistance. The larger residual Si regions are still susceptible to hydrothermal corrosion, forming large-sized pore channels that allow further water ingress. Moreover, the larger size and uneven distribution of MoSi2 hinder the formation of a continuous and uniformly distributed MoO3-SiO2 composite oxide film. Consequently, although its hydrothermal corrosion resistance surpasses that of Sample SC, the optimal improvement is not yet achieved.
Sample MS has the lowest residual silicon content (8.77 ± 0.45 vol.%) and fine, uniformly distributed MoSi2. The pores generated after hydrothermal corrosion of Si are very small; meanwhile, the fine, uniformly distributed MoSi2 forms a continuous, homogeneous MoO3-SiO2 composite oxide protective film via hydrothermal oxidation. Owing to MoO3’s much lower hydrothermal solubility, it acts as a pinning agent to retain soluble SiO2 in situ, preventing excessive dissolution and maintaining the oxide film’s compactness and stability. These two factors (minimized pore formation and effective protective barrier) synergistically block high-temperature, high-pressure water ingress, protecting the internal material from further corrosion—thus, Sample MS exhibits the lowest weight loss and shallowest corrosion depth.
Our findings demonstrate that modifying traditional RBSC materials by introducing fine and uniformly distributed MoSi2 while simultaneously reducing the residual silicon content effectively enhances hydrothermal corrosion resistance.

4. Conclusions

In this study, reaction-bonded SiC–MoSi2 composites were fabricated with the aim of enhancing the hydrothermal corrosion resistance of conventional reaction-bonded SiC ceramics through the introduction of MoSi2 and the reduction in residual silicon content. Three material systems, all prepared by reactive melt infiltration, were comparatively investigated, with the primary distinction lying in the composition and preparation route of the preforms: (i) conventional RBSC with a SiC/C preform (SC); (ii) a SiC–MoSi2 composite incorporating commercial Mo2C powder via physical mixing to obtain a SiC/Mo2C/C preform (MC); and (iii) a SiC–MoSi2 composite derived from a Mo2C/C precursor synthesized by a molten salt method, subsequently mixed with SiC powder to form the preform (MS). The microstructural evolution, phase composition, and hydrothermal corrosion behavior of each system were systematically evaluated.
(1)
The molten salt synthesis at 1150 °C yielded a Mo2C/C composite powder characterized by fine and uniformly distributed Mo2C particles intimately coated on carbon black. This contrasted sharply with the agglomerated and inhomogeneous distribution observed in the physical mixture of commercial Mo2C and carbon black. During reactive sintering at 1600 °C, the Mo2C component in both MC and MS preforms reacted with infiltrated molten silicon to form MoSi2, effectively reducing the residual silicon content. The MS sample delivered the lowest residual silicon content (8.77 ± 0.45 vol.%), followed by MC (12.43 ± 0.86 vol.%) and SC (19.17 ± 1.01 vol.%). Correspondingly, the bulk density increased from 2.96 ± 0.05 g/cm3 for SC to 3.03 ± 0.03 g/cm3 for MC and 3.07 ± 0.03 g/cm3 for MS, with all samples achieving near-full densification (open porosity < 0.1%).
(2)
From a microstructural perspective, fine MoSi2 grains were homogeneously distributed throughout the SiC matrix in Sample MS. In contrast, Sample MC suffered from partial aggregation of MoSi2 alongside residual Si, while continuous unreacted silicon regions prevailed in Sample SC. Such distinct microstructural features governed the hydrothermal corrosion performance. Hydrothermal evaluations at 345 °C and 15 MPa over 9 days confirmed a corrosion resistance trend of MS > MC > SC. After long-term exposure, the areal weight losses of SC, MC and MS were 22.3970 ± 1.2059 mg/cm2, 17.6370 ± 0.8266 mg/cm2 and 15.4347 ± 0.7807 mg/cm2, with corresponding corrosion depths of 393.17 ± 27.46 μm, 267.40 ± 24.44 μm and 224.60 ± 25.13 μm, respectively.
(3)
The enhanced performance of Sample MS is attributed to two synergistic factors. First, the substantial reduction in residual silicon content minimized the formation of large corrosion-induced pores that would otherwise serve as pathways for further water ingress. Second, the uniform distribution of fine MoSi2 grains facilitates the formation of a continuous and stable composite oxide layer of MoO3-SiO2 during hydrothermal oxidation. In this protective layer, low-solubility MoO3 exerts a pinning effect on SiO2, immobilizing it in situ and restraining its excessive dissolution. This layer exhibits superior resistance to dissolution compared to the SiO2 layer formed on unmodified RBSC, thereby effectively mitigating further corrosion of the underlying material. In contrast, the inhomogeneous distribution of MoSi2 and larger residual Si domains in Sample MC limited its protective efficiency, while the complete absence of MoSi2 in Sample SC rendered it most susceptible to hydrothermal attack.
(4)
These results demonstrate that the combination of residual silicon minimization and homogeneous incorporation of MoSi2—achieved through the use of a molten salt-derived Mo2C/C precursor in the preform—offers an effective and promising strategy for substantially improving the hydrothermal corrosion resistance of reaction-bonded SiC-based materials. It provides practical guidance for the microstructure regulation and compositional optimization of conventional RBSC fabrication processes. These findings hold significant promise for advancing the application of melt-infiltrated SiCf/SiC composites as accident-tolerant fuel cladding materials in nuclear water reactors, where superior corrosion resistance in high-temperature and high-pressure aqueous environments is critically required.

Author Contributions

Conceptualization, Y.L., Q.R.; Methodology, Y.L., Q.R.; Validation, S.C.; Data curation, S.C., H.N., X.G., T.C.; Writing—original draft preparation, S.C.; Writing—review and editing, Y.L., Q.R.; Supervision, Y.L., Q.S.; Project administration, Y.L.; Funding acquisition, Y.L., Q.H., Z.H.; Resources, Y.L., Q.H., Z.H. All authors have read and agreed to the published version of the manuscript.

Funding

This work was supported by the National Natural Science Foundation of China (Grant nos. 52302077 and 52502083), the Key Research and Development Plan Program of Ningbo (Grant no. 2025Z070), the Ningbo Natural Science Foundation (Grant no. 2024J064), the Strategic Priority Research Program of Chinese Academy of Sciences (Grant no. XDA041030301), the 3315 Innovation Team of Ningbo (Grant no. 2018A-03-A), and the Top-talent Team Program of Ningbo.

Institutional Review Board Statement

Not applicable.

Informed Consent Statement

Not applicable.

Data Availability Statement

The data presented in this study are available on request from the corresponding author due to privacy and legal reasons.

Conflicts of Interest

The authors declare no conflicts of interest.

References

  1. Lu, Y.-H.; Zhang, J.-Z.; Li, G.-Q.; Wang, Z.-H.; Wu, J.; Wei, C. A Review of Joining Technologies for SiC Matrix Composites. Materials 2025, 18, 2046. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  2. Liu, Z.-F.; Chen, X.-J.; Chen, B.-X.; Hu, Y.-M.; Zheng, K.-Y.; Liu, G.-Z.; Chen, A.-N.; Chen, P.; Li, Z.-Q.; Yang, L.; et al. The Mechanical Enhancement Mechanism in Additively Manufactured Continuous SiCf/SiC Ceramic Matrix Composites. J. Eur. Ceram. Soc. 2026, 46, 118059. [Google Scholar] [CrossRef] [Scilit]
  3. Yang, X.; Huang, Q.-Z.; Su, Z.-A.; Chang, X.; Chai, L.-Y.; Liu, C.-X.; Xue, L.; Huang, D. Resistance to Oxidation and Ablation of SiC Coating on Graphite Prepared by Chemical Vapor Reaction. Corros. Sci. 2013, 75, 16–27. [Google Scholar] [CrossRef] [Scilit]
  4. Wang, P.-P.; Li, H.-J.; Jia, Y.-J.; Zhang, Y.-L.; Yuan, R.-M. Ablation Resistance of HfB2-SiC Coating Prepared by in-Situ Reaction Method for SiC Coated C/C Composites. Ceram. Int. 2017, 43, 12005–12012. [Google Scholar] [CrossRef] [Scilit]
  5. Wang, B.; Li, G.; Li, J.-Y.; Wang, L.; Zhuang, X.-P.; Shi, W.; Tan, Y. Interfacial Modification and Oxidation Resistance Behavior of a CVD-SiC Coating for C/SiC Composites. Ceram. Int. 2023, 49, 36816–36824. [Google Scholar] [CrossRef] [Scilit]
  6. Wang, Z.-Y.; De, Y.-Y.; Wei, C.; Zhang, S.-B.; Li, X.-Q. Corrosion Behavior of NITE-SiC with Different Sintering Additives at Simulated PWRs Conditions. Ceram. Int. 2025, 51, 5725–5735. [Google Scholar] [CrossRef] [Scilit]
  7. Huczko, A.; Dabrowska, A.; Savchyn, V.; Popov, A.I.; Karbovnyk, I. Silicon carbide nanowires: Synthesis and cathodoluminescence. Phys. Status Solidi B 2009, 246, 2806–2808. [Google Scholar] [CrossRef] [Scilit]
  8. Tynyshbayeva, K.M.; Kozlovskiy, A.L. The effect of temperature factor during heavy ion irradiation on structural disordering of SiC ceramics. Opt. Mater. X 2025, 25, 100383. [Google Scholar] [CrossRef] [Scilit]
  9. Lebedev, A.S.; Suzdaltsev, A.V.; Anfilogov, V.N.; Farlenkov, A.S.; Porotnikova, N.M.; Vovkotrub, E.G.; Akashev, L.A. Carbothermal Synthesis, Properties, and Structure of Ultrafine SiC Fibers. Inorg. Mater. 2020, 56, 20–27. [Google Scholar] [CrossRef] [Scilit]
  10. Katoh, Y.; Nozawa, T.; Snead, L.L.; Ozawa, K.; Tanigawa, H. Stability of SiC and Its Composites at High Neutron Fluence. J. Nucl. Mater. 2011, 417, 400–405. [Google Scholar] [CrossRef] [Scilit]
  11. Kishimoto, H.; Katoh, Y.; Kohyama, A. Microstructural Stability of SiC and SiC/SiC Composites under High Temperature Irradiation Environment. J. Nucl. Mater. 2002, 307–311, 1130–1134. [Google Scholar] [CrossRef] [Scilit]
  12. Snead, L.L.; Nozawa, T.; Katoh, Y.; Byun, T.-S.; Kondo, S.; Petti, D.A. Handbook of SiC Properties for Fuel Performance Modeling. J. Nucl. Mater. 2007, 371, 329–377. [Google Scholar] [CrossRef] [Scilit]
  13. Lee, Y.; No, H.C.; Lee, J.I. Design Optimization of Multi-Layer Silicon Carbide Cladding for Light Water Reactors. Nucl. Eng. Des. 2017, 311, 213–223. [Google Scholar] [CrossRef] [Scilit]
  14. Agarwal, A. Structural analysis of helical coil suspension using direct optimization technique for enhanced performance. AIP Conf. Proc. 2025, 3342, 040001. [Google Scholar] [CrossRef] [Scilit]
  15. Cao, X.-Q.; Wang, J.-J.; Liang, Y.-M.; Zhang, G.-A.; Shang, L.-L.; Lu, Z.-B.; Xue, Q.-J. Corrosion and tribological investigations of the B4C coatings rubbing against SiC ball for high relative humidity engineering application. Mater. Today Commun. 2020, 23, 100924. [Google Scholar] [CrossRef] [Scilit]
  16. Hassan, R.; Balani, K. Engineered Role of SiC Particle Size on Multi-Length-Scale Wear Damage of Spark Plasma Sintered Zirconium Diboride. Adv. Eng. Mater. 2020, 22, 2000637. [Google Scholar] [CrossRef] [Scilit]
  17. Huang, C.-C.; Chen, J.; Zhu, M.; Li, F.-F.; Liu, X.-J.; Huang, Z.-R. Two-Step Joining of Reaction Bonded Silicon Carbide (RBSC) Using Borosilicate Glass. J. Mater. Res. Technol. 2023, 25, 6660–6671. [Google Scholar] [CrossRef] [Scilit]
  18. Margiotta, J.C.; Zhang, D.; Nagle, D.C. Microstructural Evolution during Silicon Carbide (SiC) Formation by Liquid Silicon Infiltration Using Optical Microscopy. Int. J. Refract. Met. Hard Mater. 2010, 28, 191–197. [Google Scholar] [CrossRef] [Scilit]
  19. Hsu, C.; Zhang, Y.; Xie, Y.; Deng, F.; Karandikar, P.; Xiao, J.Q.; Ni, C. In-Situ Measurement of SiC/Si Interfacial Tensile Strength of Reaction Bonded SiC/Si Composite. Compos. Part B Eng. 2019, 175, 107116. [Google Scholar] [CrossRef] [Scilit]
  20. Huang, Q.-W.; Zhu, L.-H. High-Temperature Strength and Toughness Behaviors for Reaction-Bonded SiC Ceramics below 1400 °C. Mater. Lett. 2005, 59, 1732–1735. [Google Scholar] [CrossRef] [Scilit]
  21. Song, N.; Zhang, H.-B.; Liu, H.; Fang, J.-Z. Effects of SiC Whiskers on the Mechanical Properties and Microstructure of SiC Ceramics by Reactive Sintering. Ceram. Int. 2017, 43, 6786–6790. [Google Scholar] [CrossRef] [Scilit]
  22. Lee, J.; Kim, D.; Shin, D.; Lee, H.G.; Park, J.Y.; Kim, W.J. A new process for minimizing residual silicon and carbon of reaction-bonded silicon carbide via chemical vapor deposition. J. Eur. Ceram. Soc. 2021, 41, 4000–4005. [Google Scholar] [CrossRef] [Scilit]
  23. Grinchuk, P.S.; Abuhimd, H.M.; Kiyashko, M.V.; Solovei, D.V.; Akulich, A.V.; Stepkin, M.O.; Evseeva, L.E. Advanced reaction-bonded SiC ceramics for space mirror blanks. J. Manuf. Process. 2024, 113, 275–290. [Google Scholar] [CrossRef] [Scilit]
  24. Chakrabarti, O.P.; Ghosh, S.; Mukerji, J. Influence of grain size, free silicon content and temperature on the strength and toughness of reaction-bonded silicon carbide. Ceram. Int. 1994, 20, 283–286. [Google Scholar] [CrossRef] [Scilit]
  25. Ren, Q.-X.; Yin, Z.-Q.; Guo, X.-Y.; Chun, S.-X.; Nie, H.F.; Yan, S.; Ru, H.-Q.; Huang, Z.-R.; Huang, Q.; Li, Y.-S. Enhanced thermal conductivity of reaction-bonded silicon carbide via constructing a mesoporous carbon network in preform. J. Mater. Sci. Technol. 2026, 262, 13–23. [Google Scholar] [CrossRef] [Scilit]
  26. Kim, W.-J.; Hwang, H.-S.; Park, J.-Y. Corrosion Behavior of Reaction-Bonded Silicon Carbide Ceramics in High-Temperature Water. J. Mater. Sci. Lett. 2002, 21, 733–735. [Google Scholar] [CrossRef] [Scilit]
  27. Xi, J.-Q.; Liu, C.; Morgan, D.; Szlufarska, I. Deciphering Water-Solid Reactions during Hydrothermal Corrosion of SiC. Acta Mater. 2021, 209, 116803. [Google Scholar] [CrossRef] [Scilit]
  28. He, F.; Liu, Y.-S.; Li, J.-X.; Liu, Q.-M.; Cao, Y.-J.; Wang, J.; Dong, N. The Impact of Water and Oxygen Contents on the Corrosion Performance of Yttrium Silicate Modified SiCf/SiC Composites under High Temperature Conditions. J. Eur. Ceram. Soc. 2024, 44, 2065–2077. [Google Scholar] [CrossRef] [Scilit]
  29. Aroati, S.; Cafri, M.; Dilman, H.; Dariel, M.P.; Frage, N. Preparation of reaction bonded silicon carbide (RBSC) using boron carbide as an alternative source of carbon. J. Eur. Ceram. Soc. 2011, 31, 841–845. [Google Scholar] [CrossRef] [Scilit]
  30. Xue, R.; Liu, P.; Zhang, Z.-J.; Zhang, N.-L.; Zhang, Y.-H.; Wang, J.-P. Improvement of toughness of reaction bonded silicon carbide composites reinforced by surface-modified SiC whiskers. Ceram. Int. 2021, 47, 18150–18156. [Google Scholar] [CrossRef] [Scilit]
  31. Li, W.; Cui, C.-C.; Li, S.; Zhang, G.; Jin, B.-J.; Bao, J.-X.; Guo, C.-H.; Zhang, Y.-B.; Liu, B.-S.; Wang, G. Vat photopolymerization of large-aperture high performance SiC mirror through multiphase carbon infiltration modification. Addit. Manuf. 2024, 85, 104160. [Google Scholar] [CrossRef] [Scilit]
  32. Zhang, H.-Z.; Zhu, Z.-B.; Huang, H.-F.; He, T.; Yan, H.-W.; Zhang, Y.-G.; Lu, Y.-P.; Wang, T.-M.; Li, T. Microstructures, Mechanical Properties, and Irradiation Tolerance of the Ti–Zr–Nb–V–Mo Refractory High-Entropy Alloys. Intermetallics 2023, 157, 107873. [Google Scholar] [CrossRef] [Scilit]
  33. Zhu, Z.-B.; Huang, H.-F.; Muránsky, O.; Liu, J.-Z.; Zhu, Z.-Y.; Huang, Y. On the Irradiation Tolerance of Nano-Grained Ni–Mo–Cr Alloy: 1 MeV He+ Irradiation Experiment. J. Nucl. Mater. 2021, 544, 152694. [Google Scholar] [CrossRef] [Scilit]
  34. Daydas, S.; Tiftikci, A. Neutronic Examination of the U–Mo Accident Tolerant Fuel for VVER-1200 Reactors. Nucl. Eng. Technol. 2024, 56, 2625–2632. [Google Scholar] [CrossRef] [Scilit]
  35. Zhang, Z.-J.; Han, E.-H.; Xiang, C. Irradiation Behaviors of Two Novel Single-Phase Bcc-Structure High-Entropy Alloys for Accident-Tolerant Fuel Cladding. J. Mater. Sci. Technol. 2021, 84, 230–238. [Google Scholar] [CrossRef] [Scilit]
  36. Ge, X.-X.; Jiang, Y.-X.; Yu, X.; Zhang, G.-P.; Shi, Y.-J.; Cai, B.; Peng, Q.; Huang, H. Preparation and Characterization of Graphene-Nanosheet-Reinforced Ni-17Mo Alloy Composites for Advanced Nuclear Reactor Applications. Materials 2025, 18, 1061. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  37. Vasudévan, A.K.; Petrovic, J.J. A Comparative Overview of Molybdenum Disilicide Composites. Mater. Sci. Eng. A 1992, 155, 1–17. [Google Scholar] [CrossRef] [Scilit]
  38. Petrovic, J.J. Mechanical Behavior of MoSi2 and MoSi2 Composites. Mater. Sci. Eng. A 1995, 192–193, 31–37. [Google Scholar] [CrossRef] [Scilit]
  39. Chang, Q.; Zhang, Q.; Xia, S.-R.; Liu, C.-D.; Cheng, L.-F.; Yu, J. Microstructure Evolution of the 5 MeV Xe20+-Implanted α-MoSi2 before and after Annealing. Ceram. Int. 2026, 52, 10266–10277. [Google Scholar] [CrossRef] [Scilit]
  40. Zhu, L.; Zhu, N.-N.; Tang, P.-J.; Zhang, B.-J.; Lei, S.-Y.; Wang, X.-H.; Feng, P.-Z. Dual Strategy to Enhance the Nitridation Resistance of MoSi2-Based Ceramics for High-Temperature Applications. J. Eur. Ceram. Soc. 2026, 46, 118155. [Google Scholar] [CrossRef] [Scilit]
  41. Lv, Y.-L.; Liu, Y.-S.; Zhang, B.-H.; Liu, M.-Z.; Fu, S.-L.; Cao, Y.-J.; Li, J.-X.; Liu, Y.-S.; Pedzich, Z. Novel MoSi2-Modified HfB2-SiC Composites Fabricated by Reactive Melt infiltration: Microstructure and Long-Term Oxidation Resistance at 1650 °C. Corros. Sci. 2026, 263, 113719. [Google Scholar] [CrossRef] [Scilit]
  42. Sun, Y.; Zheng, L.; Zhang, S.; Luo, X.; Liu, F.; Li, Y. In Situ Synthesis of Al2O3–SiC Powders via Molten-Salt-Assisted Aluminum/Carbothermal Reduction Method. Ceram. Int. 2022, 48, 24471–24475. [Google Scholar] [CrossRef] [Scilit]
  43. Yan, M.G.; Xiong, Q.-M.; Huang, J.-T.; Hou, X.-F.; Zhang, L.; Li, X.-B.; Feng, Z.-J. Molten Salt Synthesis of Titanium Carbide Using Different Carbon Sources as Templates. Ceram. Int. 2021, 47, 17589–17596. [Google Scholar] [CrossRef] [Scilit]
  44. He, M.-X.; Dong, M.-L.; Wang, C.-H.; You, Y.; Liu, P.-W. Preparation of High Purity Ti3SiC2 MAX Phase from Ti, Si, and TiC Powders by Molten Salt Method. Ceram. Int. 2025, 51, 32721–32730. [Google Scholar] [CrossRef] [Scilit]
  45. Li, F.-L.; Tan, C.; Liu, J.-H.; Wang, J.-K.; Jia, Q.-L.; Zhang, H.-J.; Zhang, S.W. Low Temperature Synthesis of ZrB2-SiC Powders by Molten Salt Magnesiothermic Reduction and Their Oxidation Resistance. Ceram. Int. 2019, 45, 9611–9617. [Google Scholar] [CrossRef] [Scilit]
  46. Yu, L.-L.; Hu, Z.-L.; Wang, Z.-Z.; Wang, H. The effect of NaOH on the morphology of dislocation-related pits in SiC during etching in molten eutectic KOH-NaOH. Mater. Sci. Semicond. Process. 2025, 192, 109437. [Google Scholar] [CrossRef] [Scilit]
  47. Winterhalter, F.; Medri, V.; Ruffini, A.; Bellosi, A. Corrosion of Si3N4-MoSi2 ceramic composite in acid-and basic-aqueous environments: Surface modification and properties degradation. Appl. Surf. Sci. 2004, 225, 100–115. [Google Scholar] [CrossRef] [Scilit]
  48. Striegler, M.; Matthey, B.; Mühle, U.; Michaelis, A.; Herrmann, M. Corrosion resistance of silicon-infiltrated silicon carbide (SiSiC). Ceram. Int. 2018, 44, 10111–10118. [Google Scholar] [CrossRef] [Scilit]
  49. Hussain, S.; Zaidi, S.A.; Vikraman, D.; Kim, H.-S.; Jung, J. Facile preparation of molybdenum carbide (Mo2C) nanoparticles and its effective utilization in electrochemical sensing of folic acid via imprinting. Biosens. Bioelectron. 2019, 140, 111330. [Google Scholar] [CrossRef] [Scilit]
  50. Etebarian, S.; Sarpoolaky, H.; Rezaie, H.R.; Velashjerdi, M. Synthesis of Ti3SiC2 MAX Phase Powder through Molten Salt Method. Int. J. Appl. Ceram. Technol. 2023, 20, 2166–2174. [Google Scholar] [CrossRef] [Scilit]
  51. Xu, J.-L.; Du, S.-Y.; Zhang, Y.-M. The Molecular Dynamic Studies of Thermal Conductivity of SiC Ceramic Derived from β/α Phase Transformation. Sci. Rep. 2025, 15, 6432. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  52. Shao, Q.-Q.; Gu, H. Transition-Layer of Core–Rim Structures and β→α Transformation in SiC Ceramics. J. Mater. 2023, 9, 299–309. [Google Scholar] [CrossRef] [Scilit]
  53. Ge, F.-F.; Zhou, M.-T.; Li, B.-S.; Yu, P.; Yan, Z.-F.; Cui, M.-H.; Shen, T.-L. Effect of the 1.52 MeV Proton Irradiation on Hydrothermal Corrosion of Sintered SiC. Corros. Sci. 2025, 252, 112964. [Google Scholar] [CrossRef] [Scilit]
  54. Motailo, E.S.; Lisyanskii, L.A.; Vikhman, S.V.; Nesmelov, D.D. Physical and Mechanical Properties of Composite Ceramics in the ZrB2-SiC-MoSi2 System. Glass Phys. Chem. 2021, 47, 646–652. [Google Scholar] [CrossRef] [Scilit]
  55. Zhang, W.-W.; Li, B.-S. Electrochemical Properties and XPS Analysis of Ni-B/SiC Nanocomposite Coatings. Int. J. Electrochem. Sci. 2018, 13, 3516–3526. [Google Scholar] [CrossRef] [Scilit]
  56. Jin, H.; Meng, S.-H.; Zhang, X.-H.; Zeng, Q.-X.; Niu, J.-H. Effects of oxygen partial pressure on the oxidation of ZrB2-SiC-graphite composites at 1800 °C. Ceram. Int. 2016, 42, 6480–6486. [Google Scholar] [CrossRef] [Scilit]
  57. Ma, Q.-Z.; Hu, R.-H.; Liu, X.-C.; Lu, X.-H.; Chen, J. Interfacial adhesion of CVD-SiC coatings on graphite substrates: Role of temperature in microstructure and mechanical properties. Ceram. Int. 2026, 52, 3711–3718. [Google Scholar] [CrossRef] [Scilit]
  58. Chen, D.; Gu, H.-Z.; Huang, A.; Ni, H.-W. Towards chrome-free lining for plasma gasifiers using the CA6-SiC castable based on high-temperature water vapor corrosion. Ceram. Int. 2019, 45, 12429–12435. [Google Scholar] [CrossRef] [Scilit]
  59. Wang, L.; Wang, S.-Y. Quantitative analysis of self-healing properties and microstructure of Ti-5Al-5Mo-5V-1Cr-1Fe alloy by quasi-in-situ XPS. J. Alloys Compd. 2025, 1012, 178509. [Google Scholar] [CrossRef] [Scilit]
  60. Zhao, H.; Xie, L.-F.; Xin, C.; Li, N.; Zhao, B.; Li, L.-Y. Effect of molybdenum content on corrosion resistance and corrosion behavior of Ti-Mo titanium alloy in hydrochloric acid. Mater. Today Commun. 2023, 34, 105032. [Google Scholar] [CrossRef] [Scilit]
  61. Zhang, B.-J.; Liu, Z.; Cheng, J.-S.; Yu, L.; Zhang, Z.-X.; Li, J.-X.; Li, S.-H.; Feng, P.-Z. In situ synthesis of Fe-Mo alloys via synergistic smelting of copper slag and spent MoSi2 rods: Phase transformation and decomposition mechanism of MoSi2. J. Mater. Res. Technol. 2025, 39, 1053–1066. [Google Scholar] [CrossRef] [Scilit]
  62. Liu, J.-X.; Wang, N.; Sun, Y.-B.; Yan, X.-B.; Wei, S.; Kang, L.; Du, B.-X.; Yang, W.-W.; Ma, K. Ability of a MoSi2 Coating to Resist Erosion-Corrosion from the Impact of Atomic Oxygen. Ceram. Int. 2025, 51, 1821–1830. [Google Scholar] [CrossRef] [Scilit]
  63. Lima, C.D.A.; De Carvalho, T.C.V.; Mendoza, C.D.; Maia Da Costa, M.E.H.; Pinheiro, G.D.S.; Luz-Lima, C.; Silva, B.G.; Sommer, R.L.; Araujo, J.F.D.F. Magnetic Transition in MoO3: Influence of Mo5+/Mo6+ Ratios on Paramagnetic to Diamagnetic Behavior. Solid State Sci. 2025, 162, 107866. [Google Scholar] [CrossRef] [Scilit]
  64. Qin, Y.-M.; Li, X.-Q.; Liu, C.-X.; Zheng, C.; Mao, Q.-P.; Chen, B.; Jing, K.; Tan, Y.-R.; Cheng, L.-F.; Zhang, L.-T. Effect of Deposition Temperature on the Corrosion Behavior of CVD SiC Coatings on SiCf/SiC Composites under Simulated PWR Conditions. Corros. Sci. 2021, 181, 109233. [Google Scholar] [CrossRef] [Scilit]
  65. Yao, Z.; Stiglich, J.; Sudarshan, T.S. Molybdenum Silicide Based Materials and Their Properties. J. Mater. Eng. Perform. 1999, 8, 291–304. [Google Scholar] [CrossRef] [Scilit]
  66. Alov, N.V. XPS Study of MoO3 and WO3 Oxide Surface Modification by Low-energy Ar+ Ion Bombardment. Phys. Status Solidi C 2015, 12, 263–266. [Google Scholar] [CrossRef] [Scilit]
  67. Yang, H.; Li, X.-Q.; Liu, C.-X.; Zhao, Y.-H.; Chen, B.; Yang, X.; Cheng, L.-F.; Zhang, L.-T. Hydrothermal Corrosion Behavior of SiCf/SiC Composites Candidate for PWR Accident Tolerant Fuel Cladding. Ceram. Int. 2018, 44, 22865–22873. [Google Scholar] [CrossRef] [Scilit]
  68. Sooby Wood, E.; Parker, S.S.; Nelson, A.T.; Maloy, S.A. MoSi2 Oxidation in 670–1498 K Water Vapor. J. Am. Ceram. Soc. 2016, 99, 1412–1419. [Google Scholar] [CrossRef] [Scilit]
  69. Terrani, K.A.; Yang, Y.; Kim, Y.-J.; Rebak, R.; Meyer, H.M.; Gerczak, T.J. Hydrothermal Corrosion of SiC in LWR Coolant Environments in the Absence of Irradiation. J. Nucl. Mater. 2015, 456, 488–498. [Google Scholar] [CrossRef] [Scilit]
  70. Shang, L.-B.; Williams-Jones, A.E.; Wang, X.-S.; Timofeev, A.; Hu, R.-Z.; Bi, X.-W. An experimental study of the solubility and speciation of MoO3(s) in hydrothermal fluids at temperatures up to 350 °C. Econ. Geol. 2020, 115, 4965–4988. [Google Scholar] [CrossRef] [Scilit]
Figure 1. XRD patterns of the composite powders synthesized by the molten salt method at different temperatures (850, 950, 1050, and 1150 °C) for 4 h: (a) full spectrum; (b) locally magnified pattern.
Materials 19 02039 g001
Figure 2. Raman spectra of commercial Mo2C and Mo2C/C composite.
Materials 19 02039 g002
Figure 3. SEM images of (a) raw carbon black, (b) physical mixture of carbon black and commercial Mo2C powder, and (c) Mo2C/C composite powder synthesized by the molten salt method at 1150 °C.
Materials 19 02039 g003
Figure 4. XRD patterns of SiC ceramic and SiC-MoSi2 composite samples after reactive sintering at 1600 °C for 2 h (SC, MC, and MS).
Materials 19 02039 g004
Figure 5. SEM images and corresponding particle size distribution maps of reactively sintered samples: (a) SC, (b) MC, (c) MS.
Materials 19 02039 g005
Figure 6. Fitted curves of corrosion weight change per unit area (∆w) for reactively sintered samples (SC, MC, MS) as a function of hydrothermal corrosion time at 345 °C/15 MPa.
Materials 19 02039 g006
Figure 7. Cross-sectional SEM images of reactive sintered SiC and SiC–MoSi2 samples after hydrothermal corrosion: Sample SC after (a1) 3 days, (a2) 6 days, (a3) 9 days; Sample MC after (b1) 3 days, (b2) 6 days, (b3) 9 days; Sample MS after (c1) 3 days, (c2) 6 days, (c3) 9 days.
Materials 19 02039 g007
Figure 8. XRD patterns of the surfaces of reactive sintered SiC and SiC–MoSi2 samples after hydrothermal corrosion (345 °C, 15 MPa) for 9 days.
Materials 19 02039 g008
Figure 9. Microstructure and EDS elemental distribution of the corroded cross-section of SC samples after 9 days of hydrothermal corrosion. (a) Cross-sectional SEM image; (b) C elemental mapping; (c) Si elemental mapping; (d) O elemental mapping; (e) EDS line-scan profiles of C, O, and Si.
Materials 19 02039 g009
Figure 10. Microstructure and EDS elemental distribution of the corroded cross-section of MC samples after 9 days of hydrothermal corrosion: (a) Cross-sectional SEM image; (b) C elemental mapping; (c) Si elemental mapping; (d) O elemental mapping; (e) Mo elemental mapping; (f) EDS line-scan profiles of C, Mo, O, and Si.
Materials 19 02039 g010
Figure 11. Microstructure and EDS elemental distribution of the corroded cross-section of MS samples after 9 days of hydrothermal corrosion: (a) Cross-sectional SEM image; (b) C elemental mapping; (c) Si elemental mapping; (d) O elemental mapping; (e) Mo elemental mapping; (f) EDS line-scan profiles of C, Mo, O, and Si.
Materials 19 02039 g011
Figure 12. XPS analysis of the surface of Sample SC after hydrothermal corrosion for 9 days: (a) survey scan spectrum, (b) high-resolution Si 2p spectrum, (c) high-resolution O 1s spectrum.
Materials 19 02039 g012
Figure 13. XPS analysis of the surface of Sample MC after hydrothermal corrosion for 9 days: (a) survey scan spectrum, (b) high-resolution Si 2p spectrum, (c) high-resolution Mo 3d spectrum, (d) high-resolution O 1s spectrum.
Materials 19 02039 g013
Figure 14. XPS analysis of the surface of Sample MS after hydrothermal corrosion for 9 days: (a) survey scan spectrum, (b) high-resolution Si 2p spectrum, (c) high-resolution Mo 3d spectrum, (d) high-resolution O 1s spectrum.
Materials 19 02039 g014
Figure 15. Schematic structure diagram of the hydrothermal corrosion mechanism of SC, MC, and MS samples.
Materials 19 02039 g015
Table 1. EDS point analysis results (at.%) for the marked regions in the SEM images shown in Figure 3.
PositionMoC
Point 132.367.7
Point 28.291.8
Point 310.789.3
Point 42.397.7
Table 2. Residual Si contents and densification results of SC, MC, and MS samples after reactive sintering at 1600 °C for 2 h.
SampleResidual Si Content (vol.%)Bulk Density (g/cm3)Open Porosity (%)
SC19.17 ± 1.012.96 ± 0.050.05 ± 0.02
MC12.43 ± 0.863.03 ± 0.030.03 ± 0.01
MS8.77 ± 0.453.07 ± 0.030.02 ± 0.02
Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content.