1. Introduction
The bio-economy encompasses all activities related to the production and transformation of biomass, whether of agricultural, forestry, or aquaculture origin, for the purposes of food production (human or animal), bio-based chemistry, bio-based materials, or energy [
1,
2]. Hence, biorefineries are being developed as technological means for the transition to this economic approach, opening the opportunity to add value to biomass through more sustainable production [
3]. Sustainable development has become the key of the 21st century in the search for a green engineering process. Considerable importance is attached to the use of renewable raw materials like vegetable oils. Due to environmental considerations concerning sustainable development and others, like their possible contribution to regional development and supporting agriculture in times of surplus production, renewable resources are currently attracting increasing interest as raw material for industry.
In this sense, the synthesis process itself has strong potential to develop further and provide a core tool for the application of new innovative technology. Furthermore, process integration can be used to maintain low costs and thus aid these processes in being competitive in a market presently dominated by products produced from other sources of raw materials, specifically fossil fuels such as petroleum and natural gas [
4]. Chemical processes that include environmental issues in the selection of reagents and reaction conditions are increasingly gaining importance as both industrial and academic researchers take notice of the “green” or environmentally friendly approach [
5].
Fats and oils based on lauric acid (dodecanoic acid) have attracted a great deal of interest in recent years [
6]. Coconut oil pertains to a unique group of vegetable oils known as lauric oils. The most common fatty acid in this group is lauric acid, with most coconut oils generally containing between 46% and 49% lauric acid [
7]. Coconut (
Cocos nucifera L.) is cultivated in about 93 countries, with the largest cultivation areas and exporting countries being Indonesia, the Philippines, India, and Malaysia [
8]. At present, 90% of the world’s supply is from Asia, where it is a major source of revenue for several countries. A major natural product produced from the nut (copra) is coconut oil [
9].
Ethanol and butanol are derived from agricultural products [
10,
11]; they are renewable and environmentally less bio-objectionable sources of energy [
12]. Ethanol and butanol fermentation (ABE) has attracted renewed interest recently in the sense of biorefinery approaches for the obtention of fuels and chemicals from renewable resources [
11]. In comparison to methanol, ethanol and butanol are safer to handle, as the human toxic effects of fume expose are minimized [
13].
The production of ethyl and butyl esters instead of methyl esters is of great interest, as it offers the possibility of obtaining a fuel that is fully an agro-fuel [
14]. In addition, biobutanol, which is produced from renewable sources, is a molecule that has more energy than ethanol and is less soluble in water but with the inconvenience of being more toxic [
15].
Aviation is still a major cause of climate change, even with recent advances in fuel efficiency [
16]. This sector, responsible for 2.1% of all man-made CO
2 emissions and 12% of all transport-related emissions, is already the world’s second largest source of greenhouse gases [
17,
18]. With the increasing demand for air transport, emissions from international aviation are projected to increase threefold by 2050 [
19,
20]. Bio-jet fuel (BJF) or Sustainable Aviation Fuels (SAF) is key to significant and immediate reductions in aviation’s carbon footprint [
21].
BJF is proposed as an alternative to reach a balance between sustainability and service [
22,
23]. BJF is a non-petroleum jet fuel that is made by recycling sustainable feedstocks, agricultural residues, sawdust, or wastewater, including used cooking oil, which, while it would normally be disposed of, may be used as a valid feedstock to produce BJF [
24,
25].
It should be pointed out that the type of feedstock influences the final product quality and properties [
26]. L.N. Silva et al. have investigated the possibility of making biokerosene from macauba oils by a catalytic deoxygenation reaction [
27]. Non-edible sunflower oil also has been employed as a feedstock for BJF production by a catalytic process, which yielded carbon chains of approximately C7 and C43 [
28].
This mixture can be applied not only to the production of BJF but also to renewable gasoline, diesel, and heavier fractions for marine engines. BJF containing n-paraffins, isoparaffins, and aromatic compounds has been produced from inedible soybean oil [
29]. Lignocellulosic biomass could be converted to BJF by flash pyrolysis or hydrodeoxygenation (HDO) [
30]. Thus, it has been reported that straw as a feedstock has been converted via flash pyrolysis into C8–C15 hydrocarbons meeting the technical specifications of jet fuels [
31]. Y. K. Chen et al. produced BJF via the same process using rice husk as feedstock [
32]. Microalgae are another potential feedstock for jet fuel production via the hydrothermal liquefaction process [
33]. In order to further develop the circular economy, new options such as plastic waste could be important sources of raw material to be processed into BJF [
34,
35]. In this regard, W. Mateo et al. were able to transform biomass and plastic waste via catalytic pyrolysis into BJF (aromatics and C9–C16 alkanes) [
36]. Mei Yin Ong and co-workers were able to produce bio-kerosene (biofuel), which is a renewable fuel to operate a gas turbine engine, via vacuum distillation of a mixture of biodiesel (fatty acid ethyl esters) from microwave-assisted trans-esterification of coconut oil with ethanol [
37]. The optimum biofuel production yield for jet was 74.45%, obtained with an ethanol-to-oil molar ratio of 9.25:1 under microwave irradiation (163.69 W) for 12.66 min. The authors also revealed that the biofuel produced had properties compared to the American Society for Testing and Materials (ASTM) D1655 standard. Afterward, the authors used modeling (Response Surface Methodology and Artificial Neural Network Methodology) to optimize this process. Thus, catalytic hydrotreatment of esters and/or fatty acids represents the most established route to produce jet biofuels. This process is conducted via several reactions: hydrodeoxygenation, hydrocracking, and hydro-isomerization, depending on the chemical composition of the feedstock, the catalyst used, and the desired fuel properties. In the case of heterogeneous processes, these transformations of esters and fatty acids are generally carried out under H
2 pressures and high temperatures. Rodolpho R. C. Monteiro presented a bibliographic synthesis about the catalytic hydrotreatment of esters, whether through heterogeneous or enzymatic catalysis, together with the main materials used [
38].
Recent research in aviation decarbonization has shifted from the pursuit of generic biodiesel production toward the development of specialized niche feedstocks capable of yielding specific drop-in fuels. Unlike conventional methods that produce broad mixtures of fatty acid esters, there is an increasing demand for targeted processes that can tailor the molecular composition of fuels to meet the rigorous physical and chemical requirements of jet-grade kerosenes.
Enzymatic transesterification reactions employing lipases present several advantages compared to conventional catalysts: they display higher selectivity, can operate under mild reaction conditions, exhibit few side reactions, and yield products of high purity [
39].
Lipases can catalyze esterification, inter-esterification, and transesterification reactions in non-aqueous environments. This great feature and the protein engineering progress have caused lipases to become one of the most used enzymes by industry. The lipases hydrolyze triacylglycerols at the aqueous-nonaqueous interface; however, these enzymes may also catalyze the production of esters from long-chain fatty acids and alcohols in a low humidity environment [
40].
Taking a closer view of the catalytic mechanism, lipases perform a two-step mechanism for the formation of fatty acid alkyl esters in transesterification reactions, typically by means of the Ping-Pong Bi-Bi mechanism [
41]. In the transesterification reaction, the acyl group of the ester or triacylglycerol is replaced with the alkyl groups of a nucleophilic agent, typically an alcohol, and is therefore called alcoholysis. It is one of the more important and commonly used reactions industrially, especially in the biodiesel reaction.
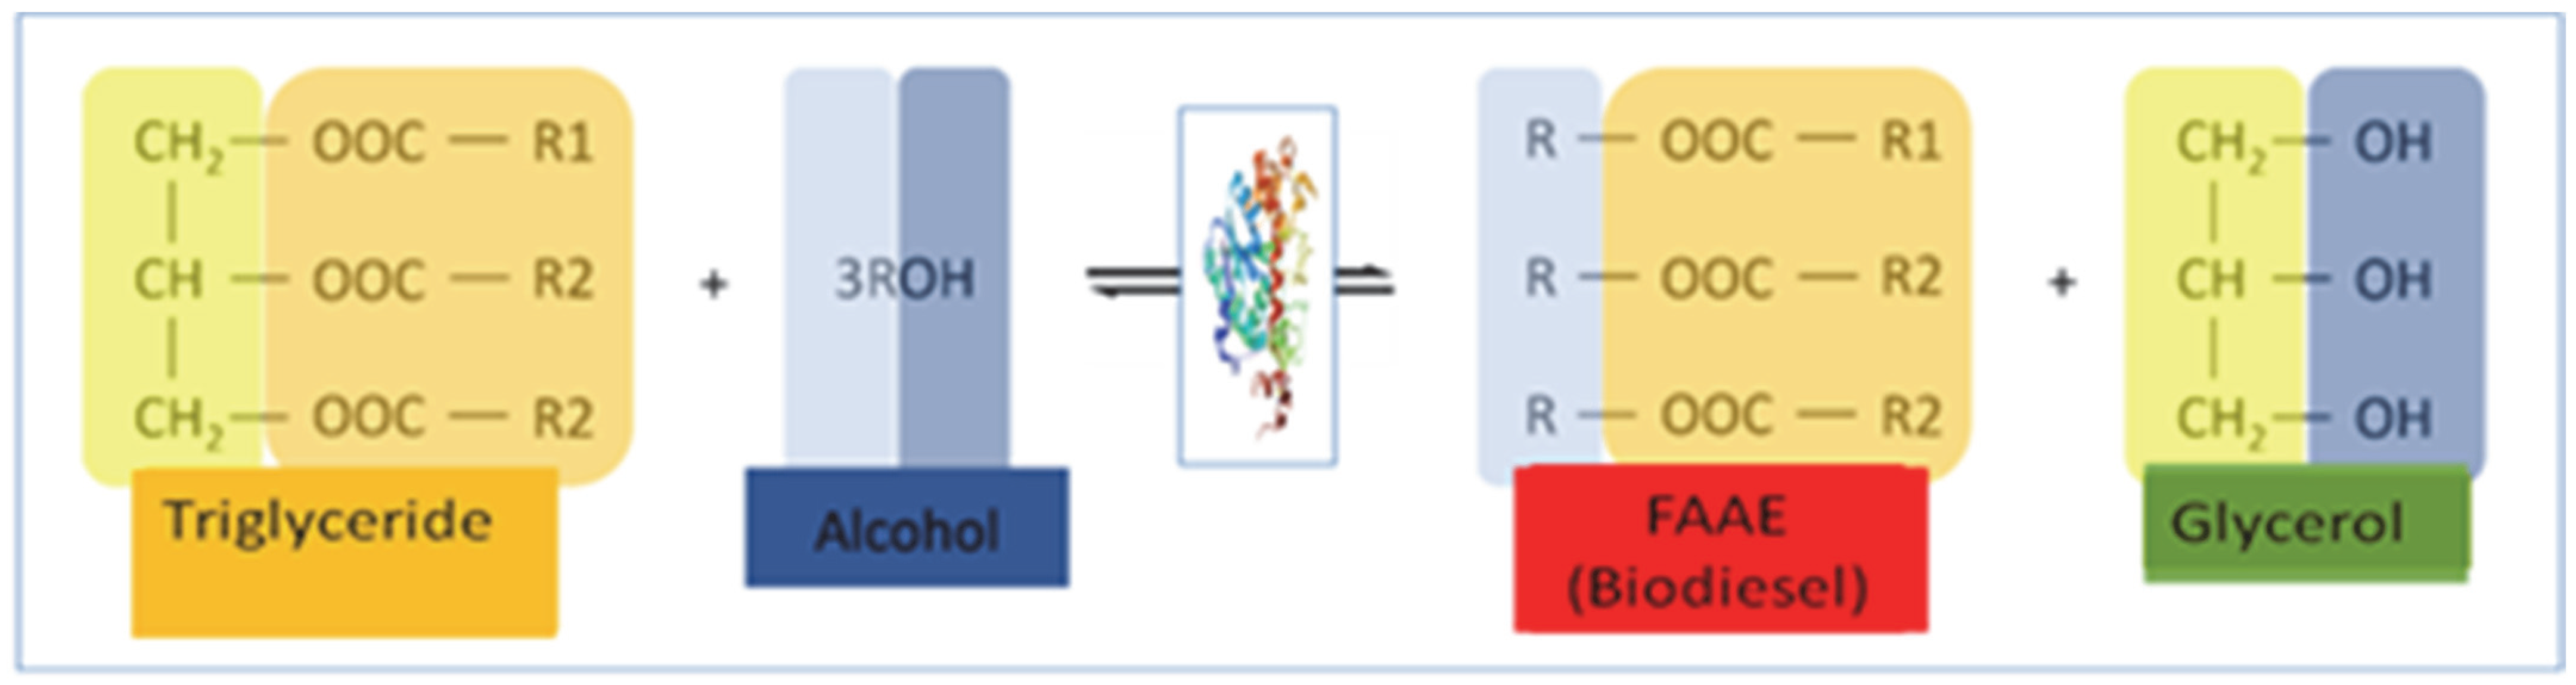
Figure 1 shows the complete process converting triacylglycerols to biodiesel and glycerol-like end products. Like any biochemical reaction, the reversed synthesis reaction also occurs at the molecular scale. The lipase specificity varies depending on the length of the fatty acids, the double bonds, and the presence of branched groups, and, as a consequence, the reaction rates can vary significantly depending on the composition of the triglycerols. Lipases are particularly effective against medium- to long-chain fatty acids, which are the most common in biofuel production [
42].
Certain lipases are non-specific and are able to act on any of the ester bonds of triglycerols and thus cleave the triglycerols to liberate free fatty acids and glycerol-like end products. Enzymes can therefore turn out a large range of substrates and catalyze a wide variety of different types of reactions and therefore have many applications in the pharmaceutical, food, detergent, and biofuel industries [
43].
In fact, the stability and reusability of lipases under the conditions used in biofuel production are limited. The process is more time consuming than using alkaline catalysis, and, in many cases, yields are lower as well. To feed the multi-billion-dollar enzyme market, various enzyme formulations are offered by big companies for large-scale industrial process applications. In the energy sector for biofuel production (e.g., biodiesel and 2G ethanol), new enzyme formulations with improved stability and functionality are regularly introduced into the market. Recent studies on lipases have shown an improved enzyme recyclability of up to 12 times and an increasing yield of biodiesel from soybean oil (97%), indicating promising results in the field of biofuels [
44]. Enzymatic catalysis for BJF production appears to be a great alternative with numerous advantages due to their high selectivity as well as the need for mild operational conditions.
In order to improve the sustainability of the process and reduce production costs, an enzymatic catalysis will be used that allows working at lower temperatures and pressures (ideally at atmospheric pressure) and that also reduces or completely avoids the use of H2.
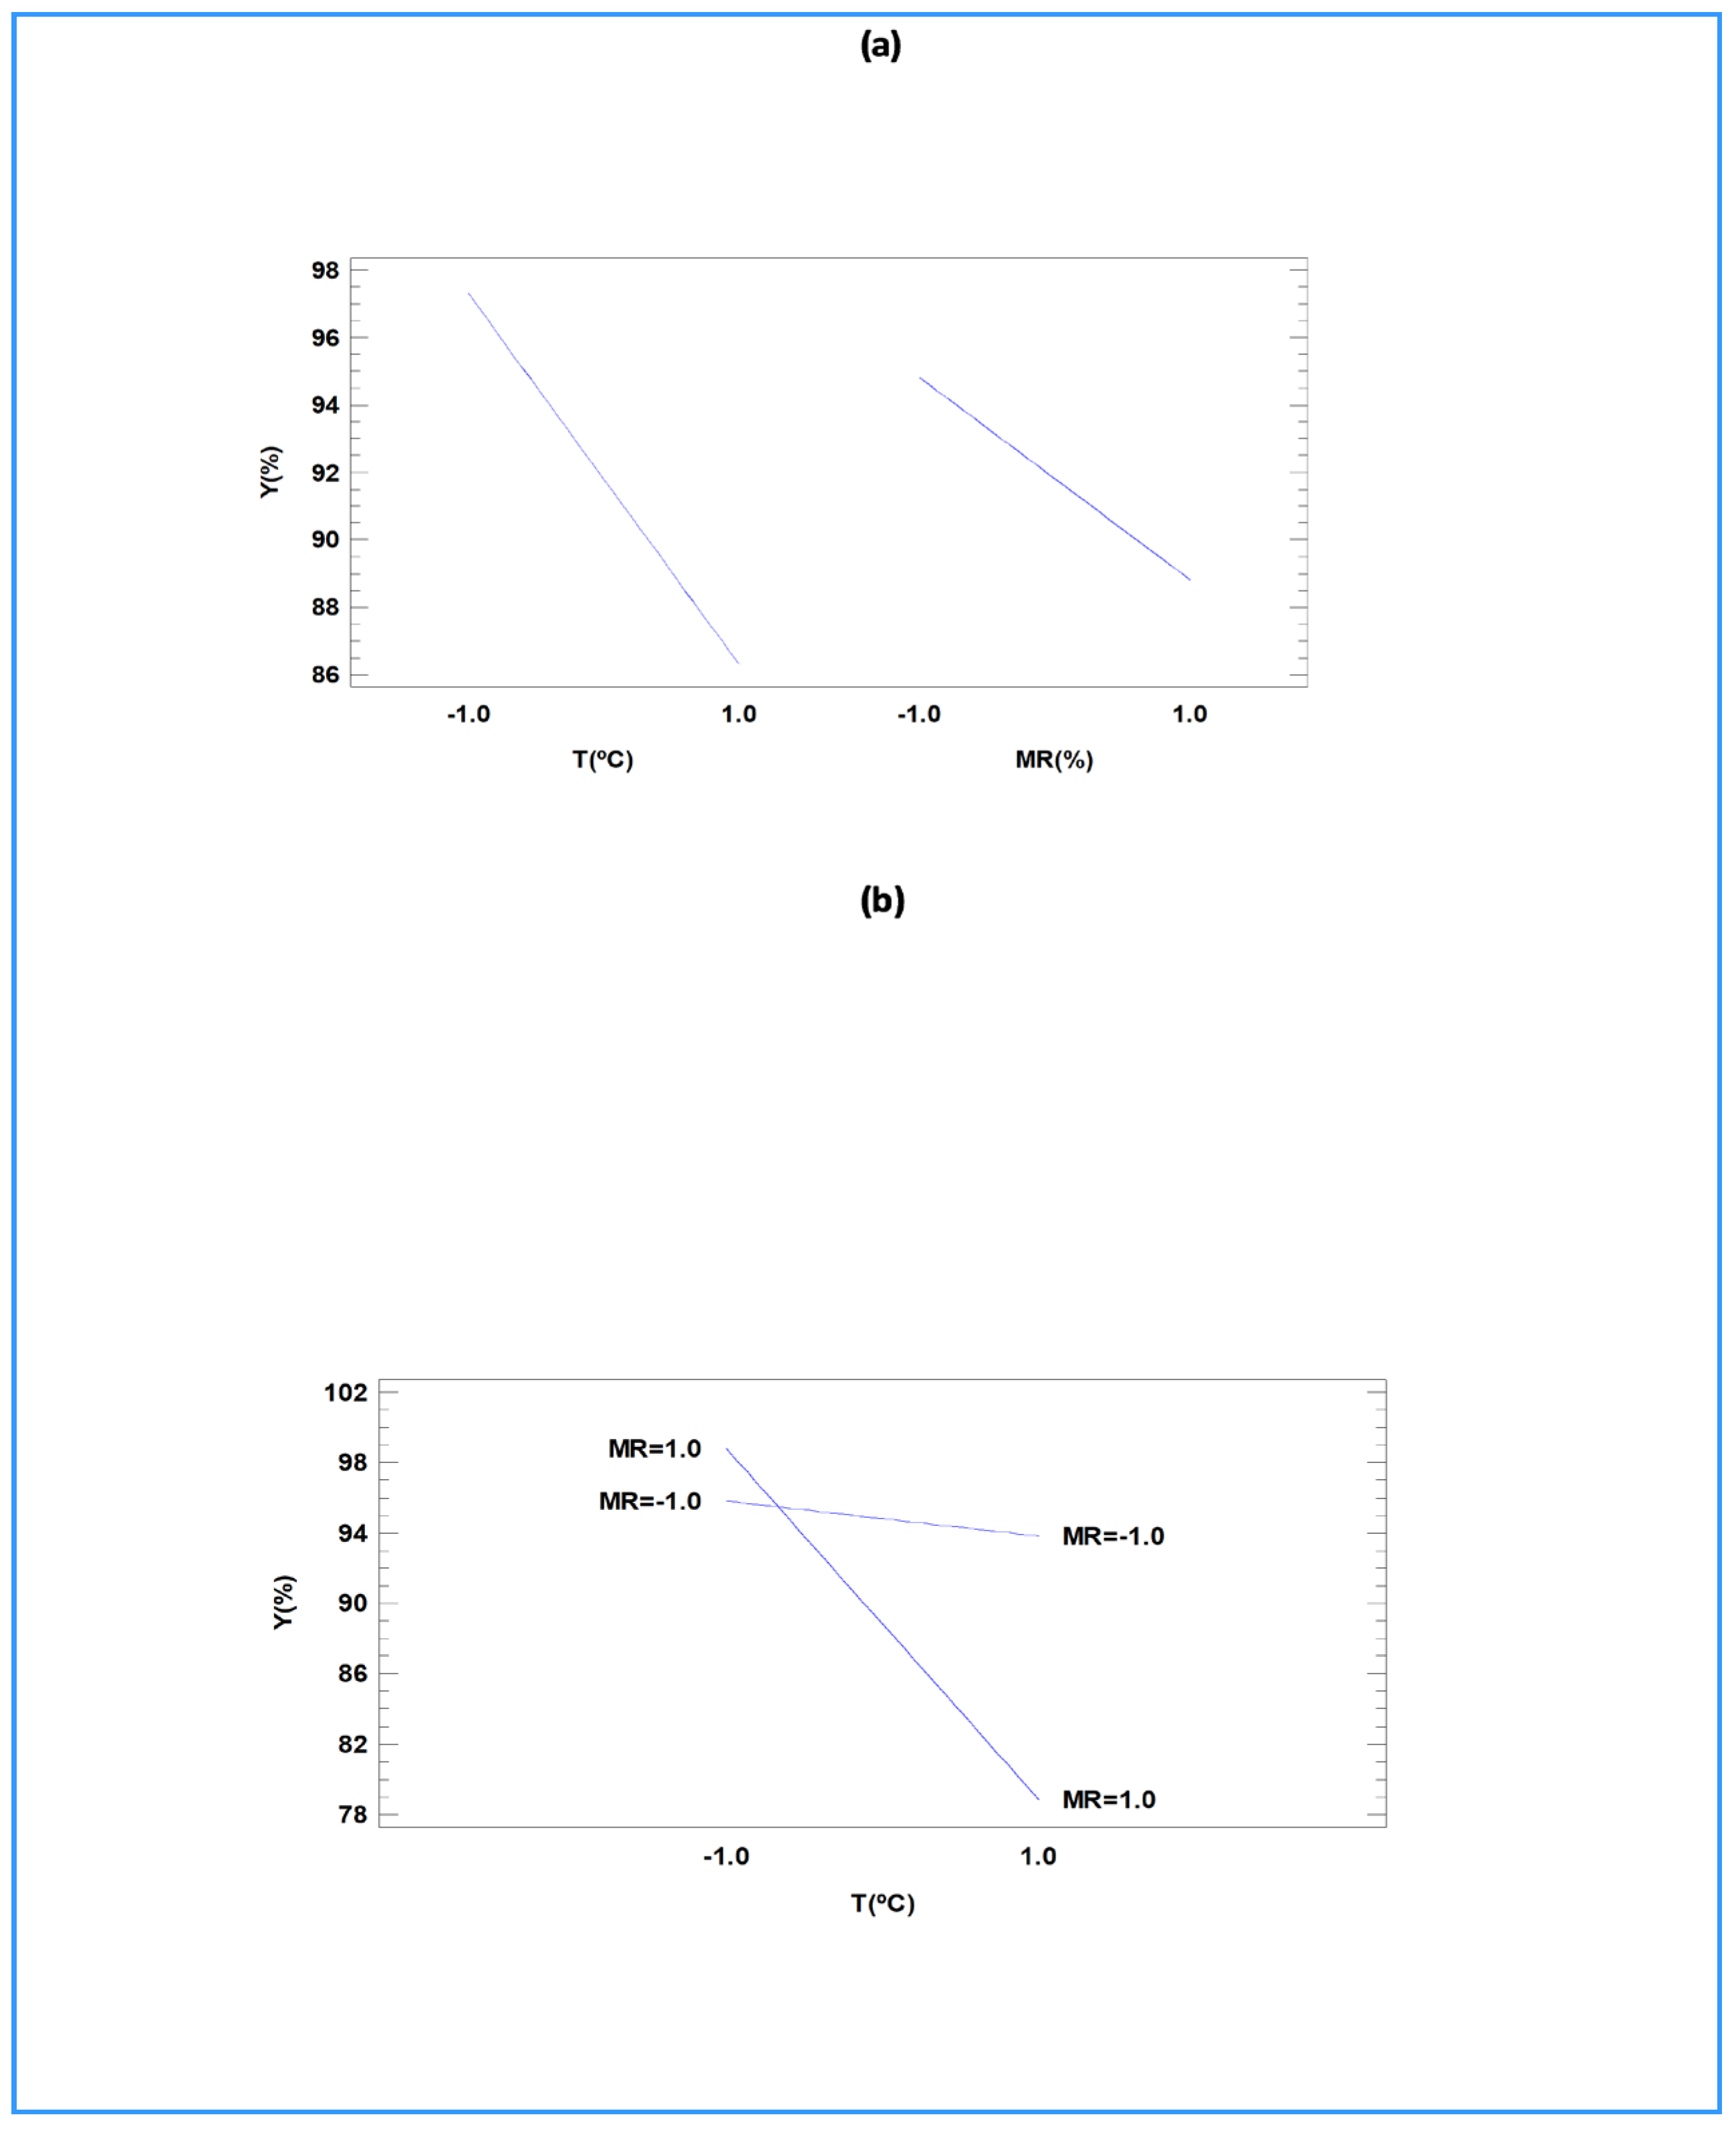
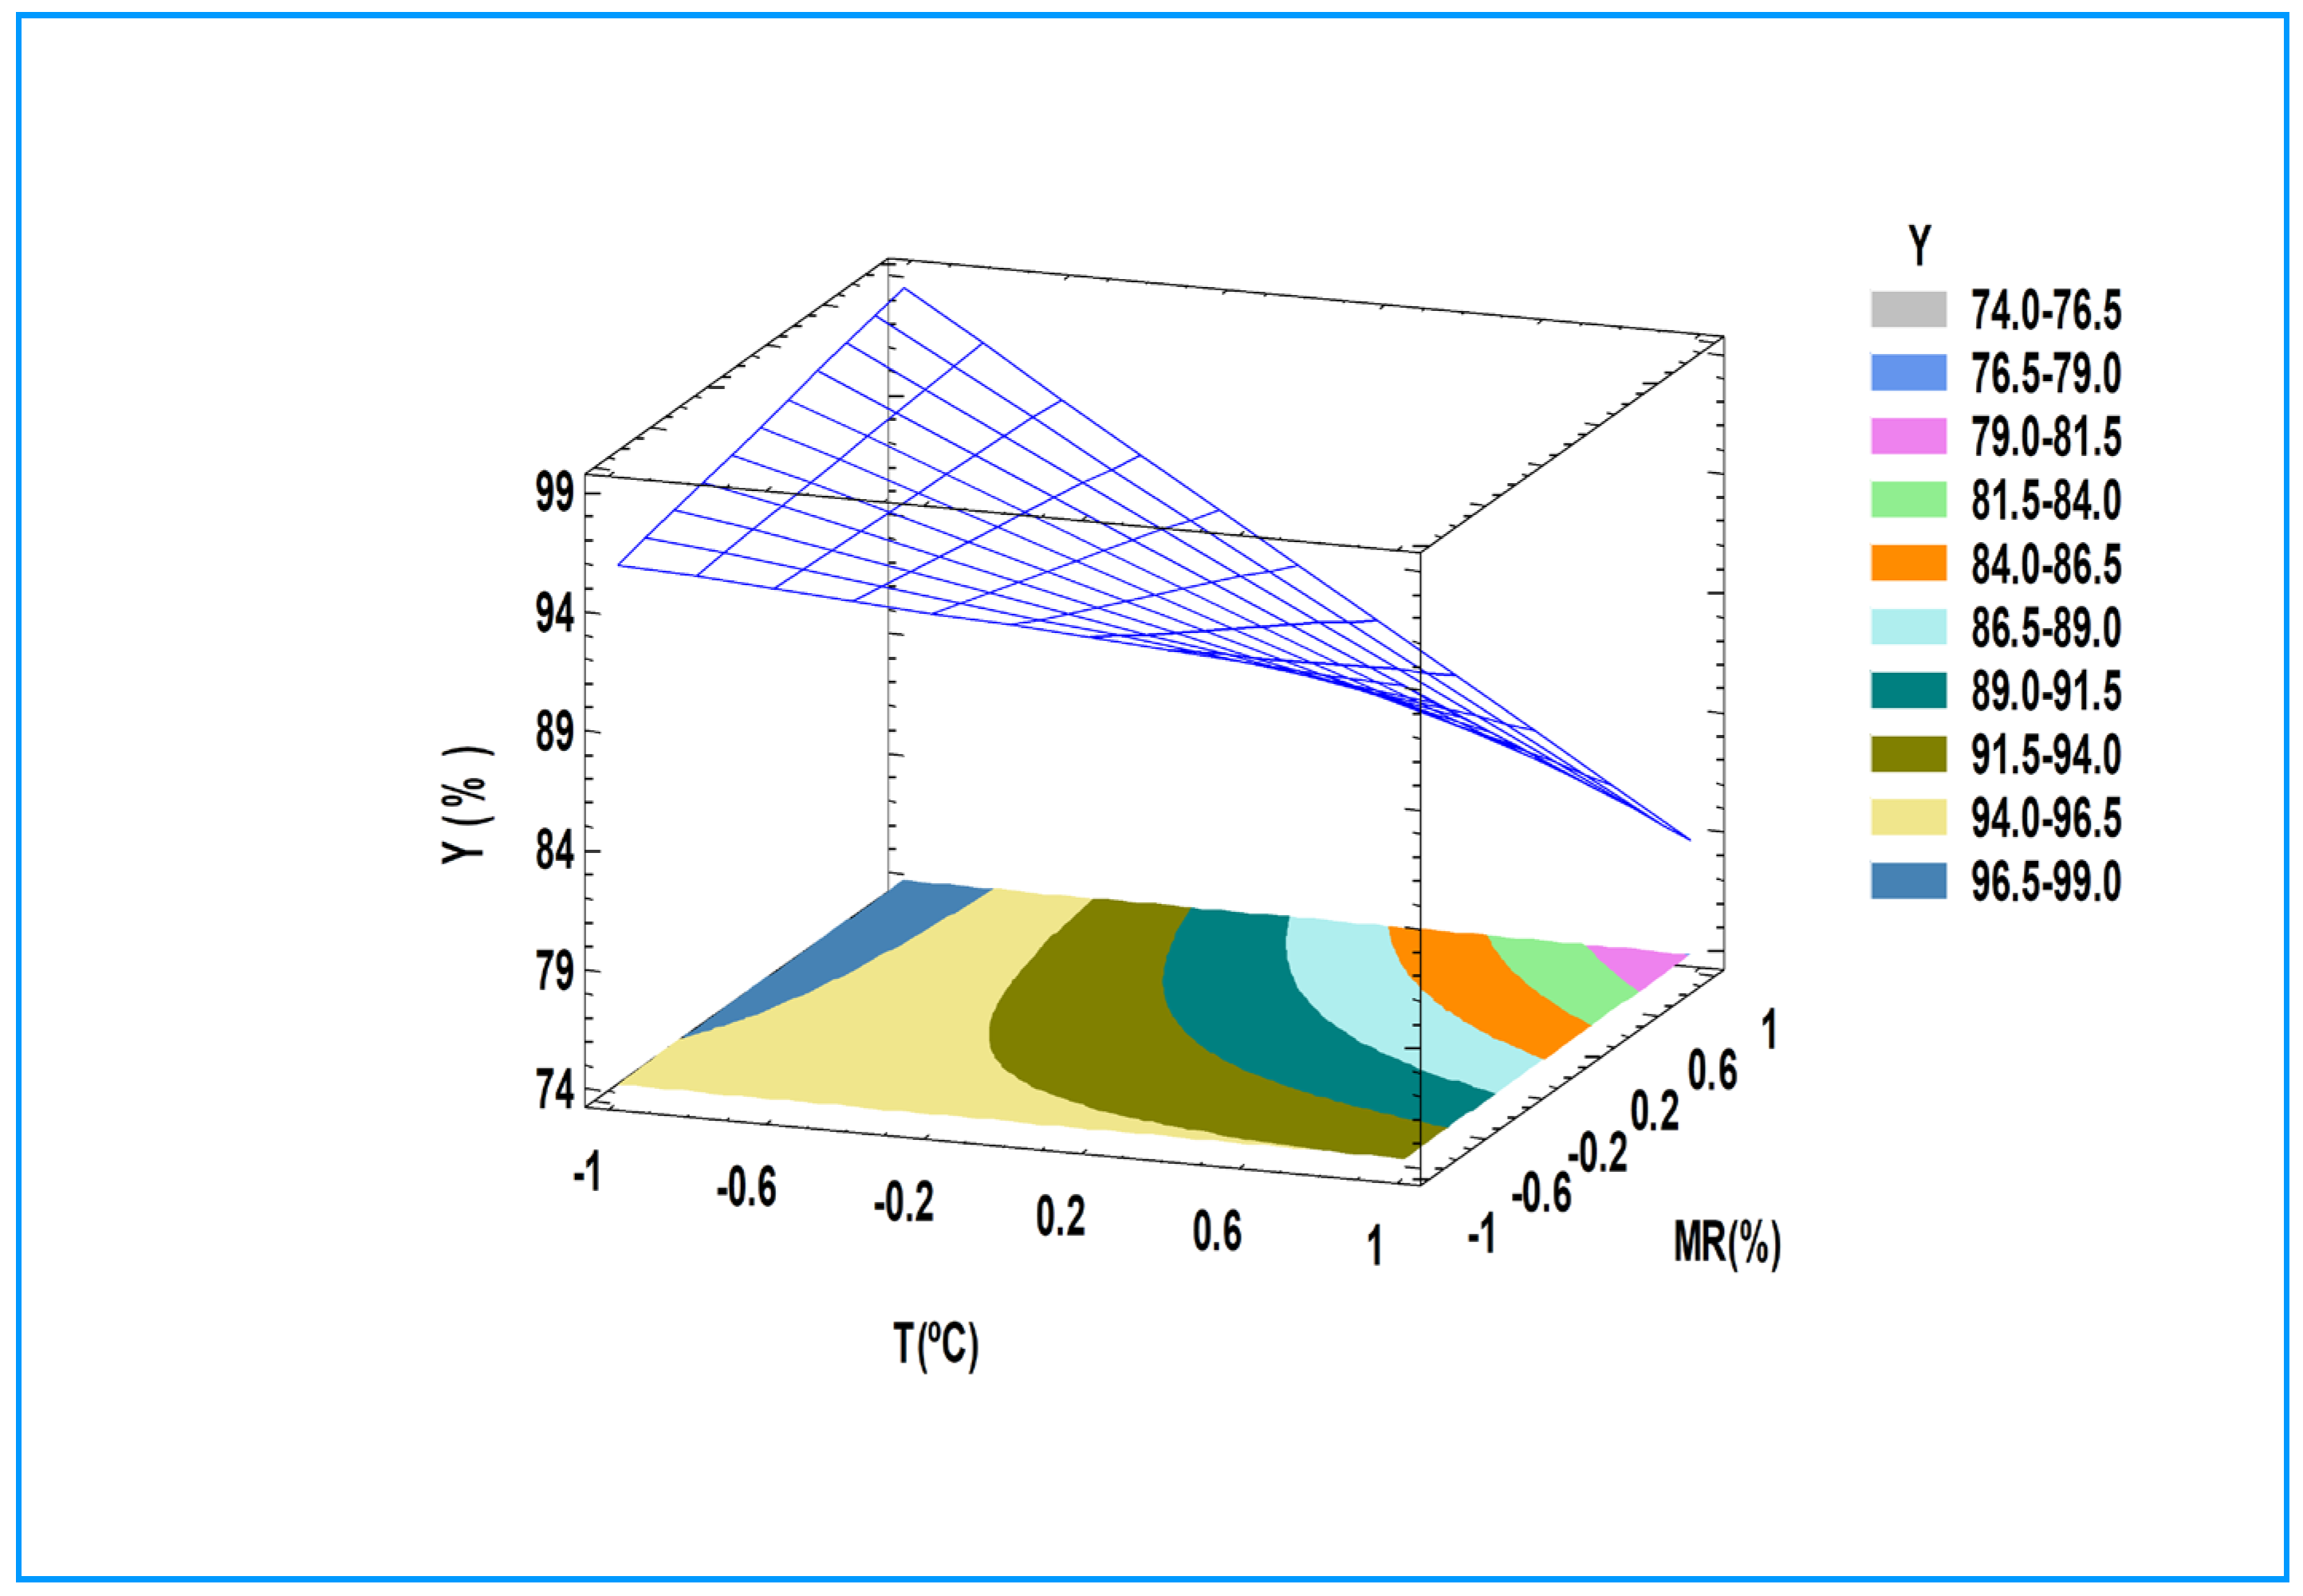
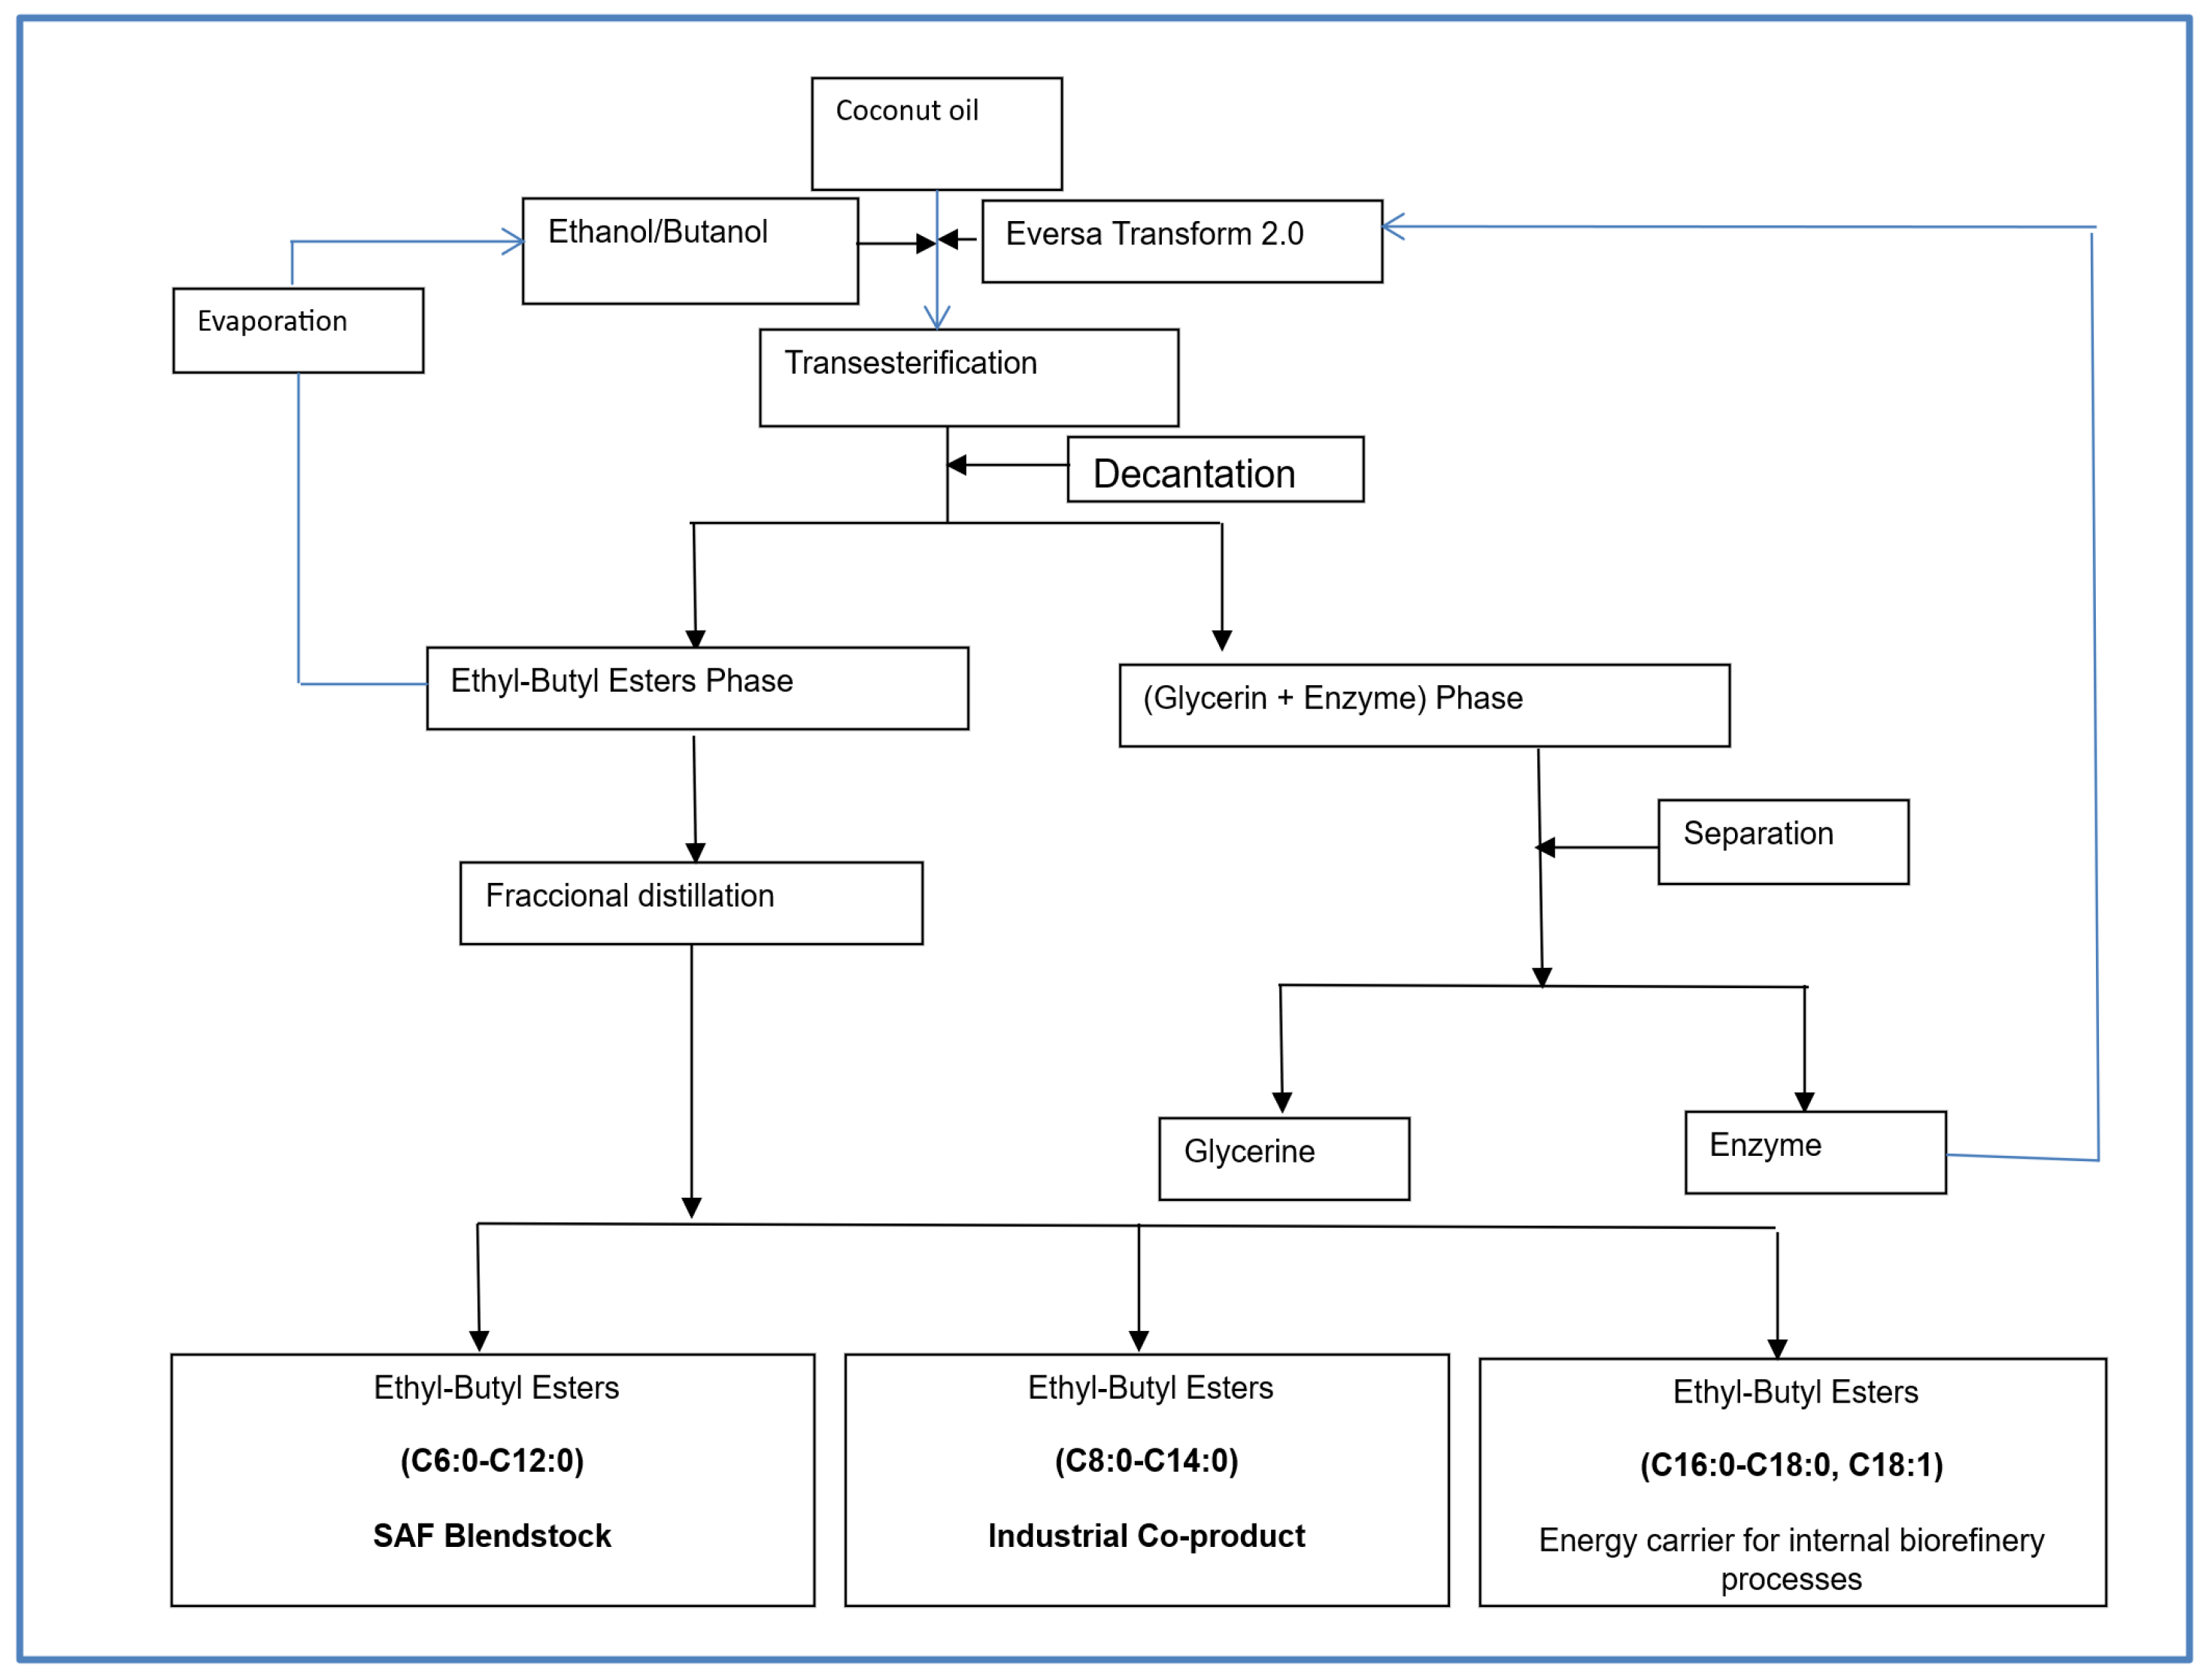
Within this framework, the present study proposes an integrated biorefinery pathway for the selective production of SAF precursor blendstocks and high-added-value biochemicals through the enzymatic transesterification of coconut oil. A key innovation of this work is the application of a synergistic ethanol-butanol binary system, strategically employed to manipulate the ester molecular structure, thereby addressing the stringent low-temperature performance requirements of the aviation sector. Furthermore, the transesterification process was rigorously optimized using a Design of Experiments (DoE) framework, combining factorial design and Response Surface Methodology (RSM). This systematic approach ensures optimal control over reaction variables, maximizing both process efficiency and carbon atom economy while minimizing research time, energy consumption, and environmental waste.
The choice of a coconut lipid matrix is dictated by its unique fatty acid profile, which naturally contains over 60% short–medium-chain saturated fatty acids (C6–C12), a distribution completely absent in waste cooking oils or jatropha (predominantly C18). To ensure economic viability and avoid food-vs.-fuel conflicts, this process targets low-grade Coconut Fatty Acid Distillates (CFAD), a non-edible refining waste. Economically, the high cost of the lipid feedstock is amortized by the cascading design: the extraction of the specialty chemical fraction (C8–C14) targets high-margin markets, effectively subsidizing the production cost of the biofuels stream.
4. Discussion
4.1. Synergistic Engineering of Cold Flow Properties via Ethanol-Butanol Binary System
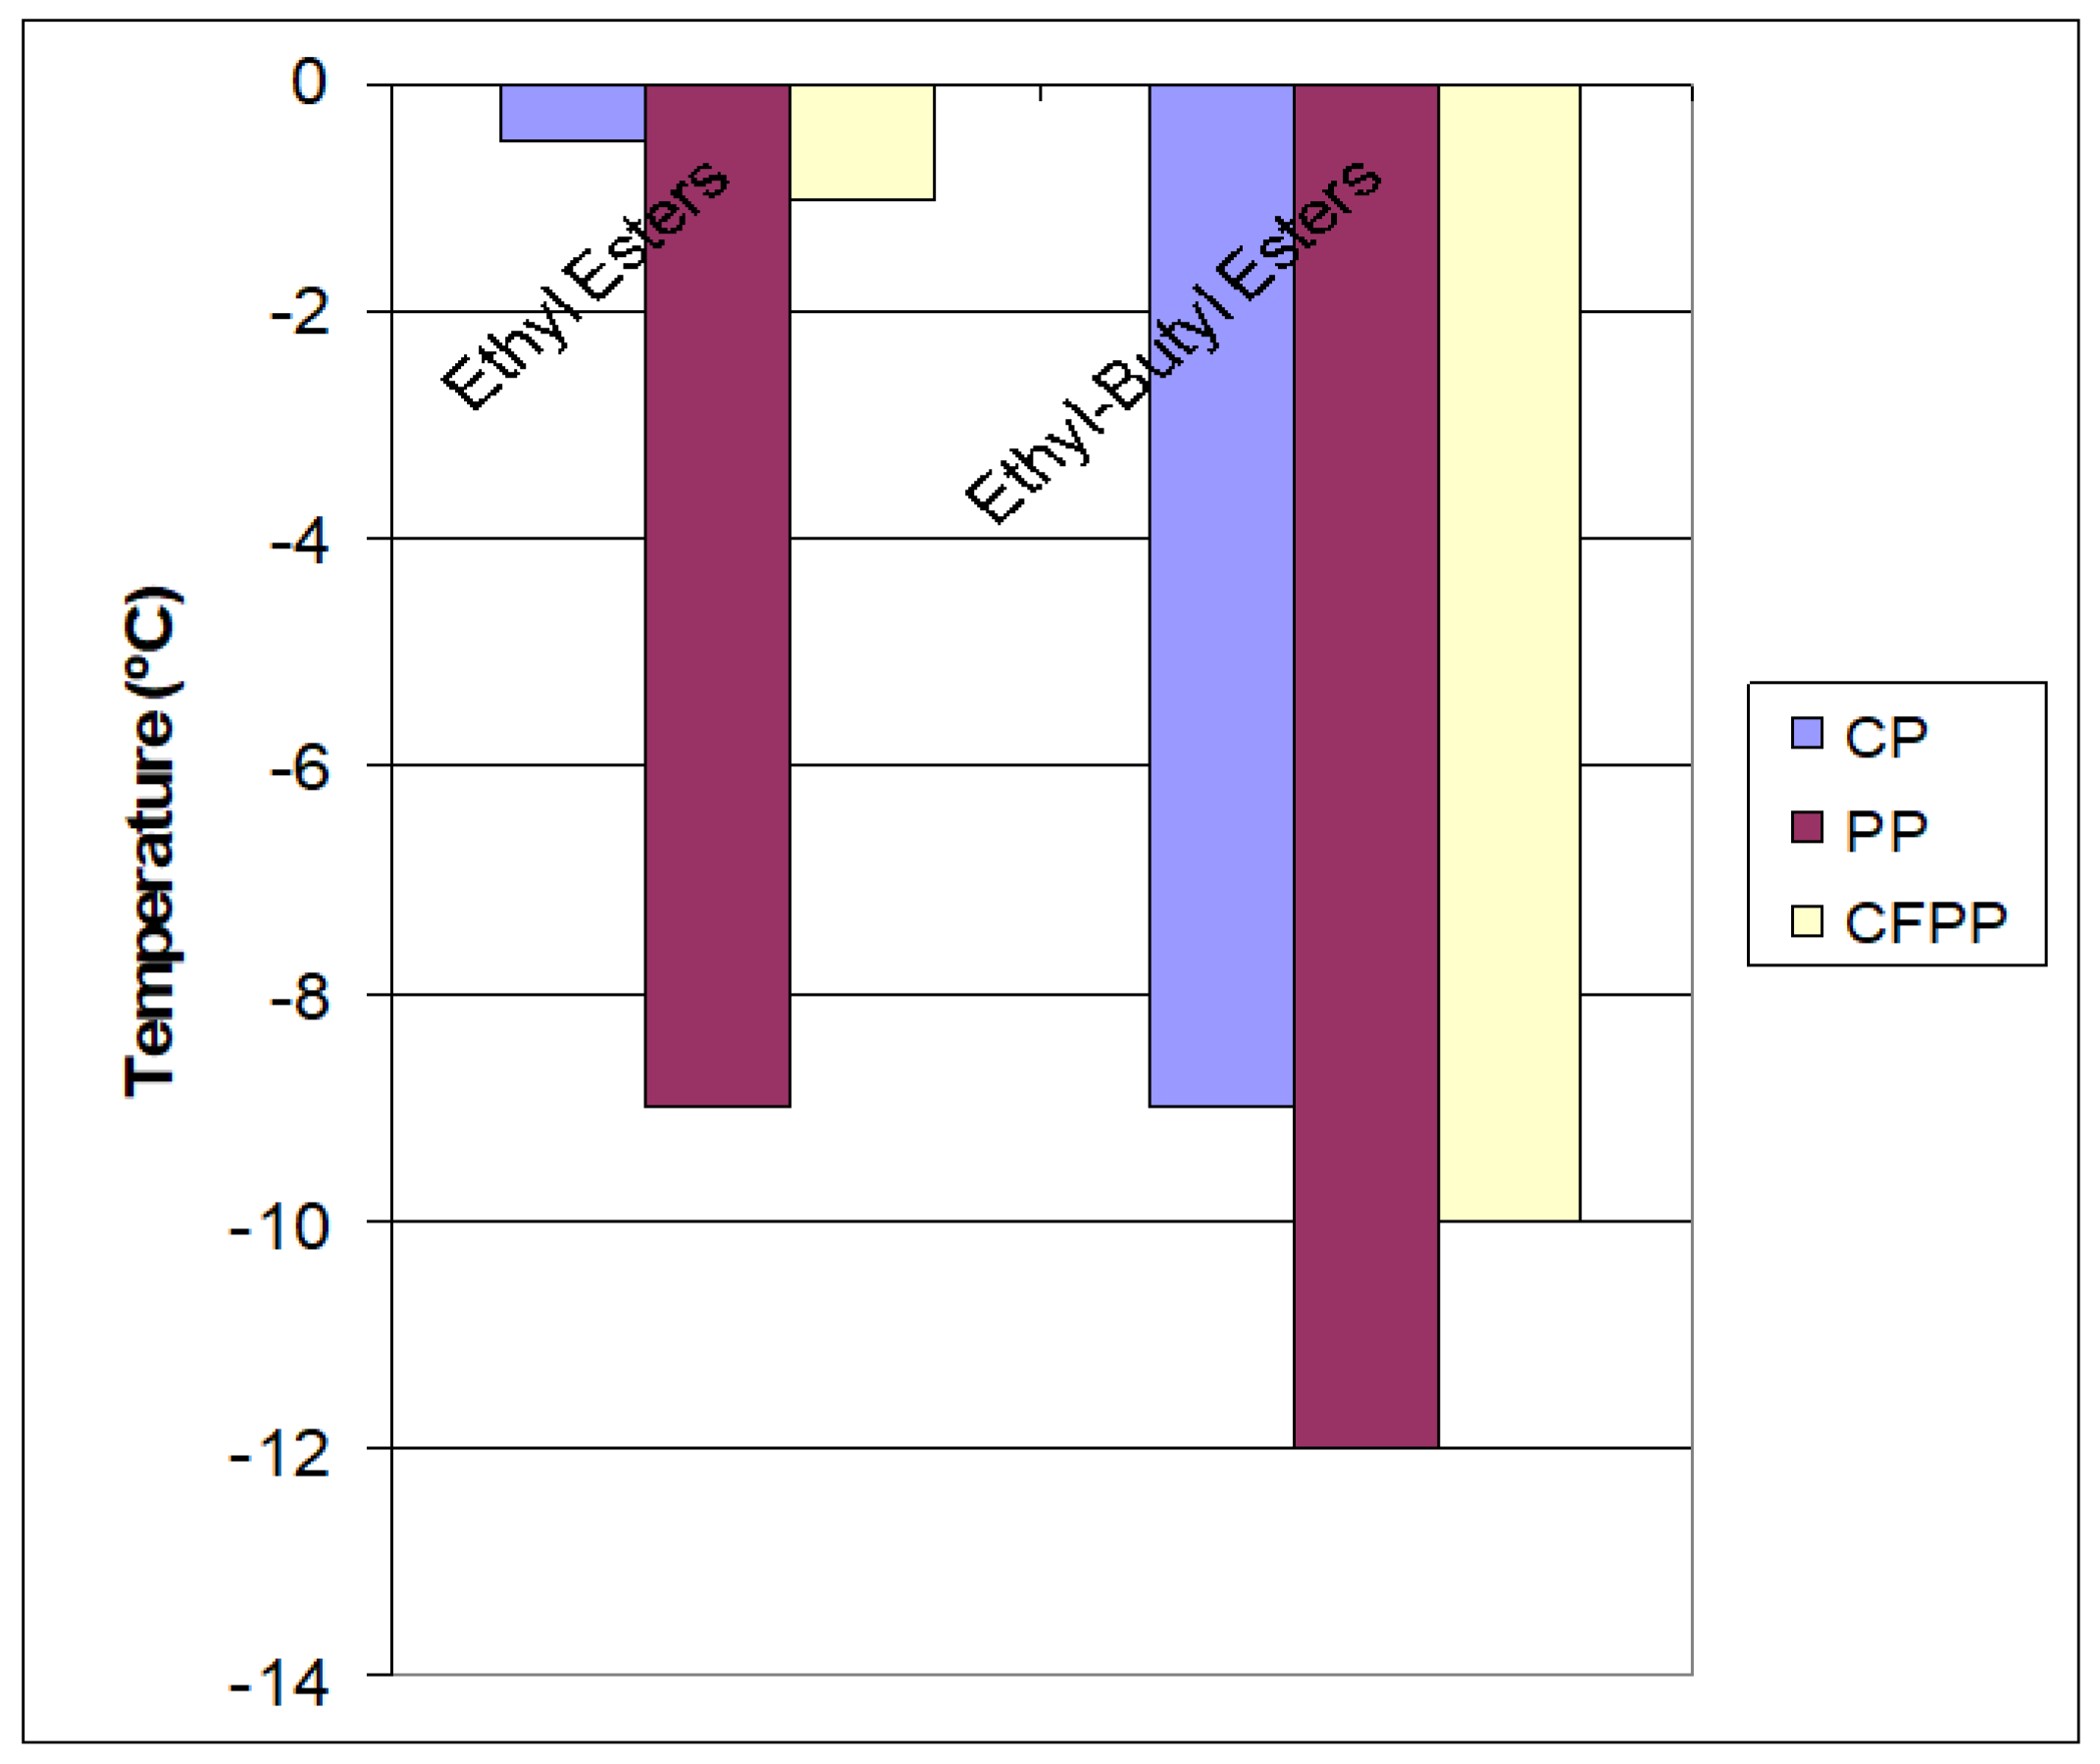
A fundamental challenge in utilizing coconut oil-derived esters for aviation applications is the high concentration of saturated fatty acids (C12:0 and C14:0), which tends to promote high crystallization temperatures, leading to poor cold-flow performance. Our findings demonstrate that the implementation of a binary ethanol-butanol system effectively bypasses these limitations by strategically modulating the molecular architecture of the final ester matrix. The significant depression of the cloud point (CP) and pour point (PP) observed in the ethyl-butyl ester (EBE) mixture, compared to conventional FAEEs, is driven by two synergistic mechanisms:
Molecular Disruption of Crystal Packing: The introduction of the C4 (butyl) moiety into the ester backbone creates structural asymmetry compared to the linear C2 (ethyl) group. This increased steric hindrance disrupts the tight packing of the saturated molecular crystal lattice. By increasing the configurational entropy of the mixture, the system requires lower temperatures to reach the liquid-to-solid phase transition, effectively suppressing the formation of crystalline wax structures.
Enhanced Biocatalytic Environment: As discussed in
Section 3.2, the binary alcohol system optimizes lipase performance. While pure ethanol acts as a strong polar solvent capable of stripping the enzyme’s essential hydration layer, the presence of butanol serves as a hydrophobic buffer. This stabilizes the Eversa Transform 2.0 active site, ensuring a highly selective transesterification process that produces a more heterogeneous ester profile, further contributing to low-temperature stability. The effectiveness of this “molecular tailoring” is evidenced by the cold-flow performance of the isolated C6–C12 Bio-Jet Fuel (BJF) precursor fraction. As summarized in
Table 6, the EBE fraction exhibits a pour point of −12 °C, representing a significant improvement over the −9 °C observed in pure coconut FAEE. This outcome indicates that adjusting the alcohol chain length is a highly effective, green strategy to align bio-derived fractions with the stringent low-temperature requirements of the ASTM D7566 standard. By achieving these properties natively, this process minimizes the reliance on synthetic pour point depressants (PPDs), thereby simplifying the refinery downstream processing and enhancing the overall environmental sustainability of the SAF production chain.
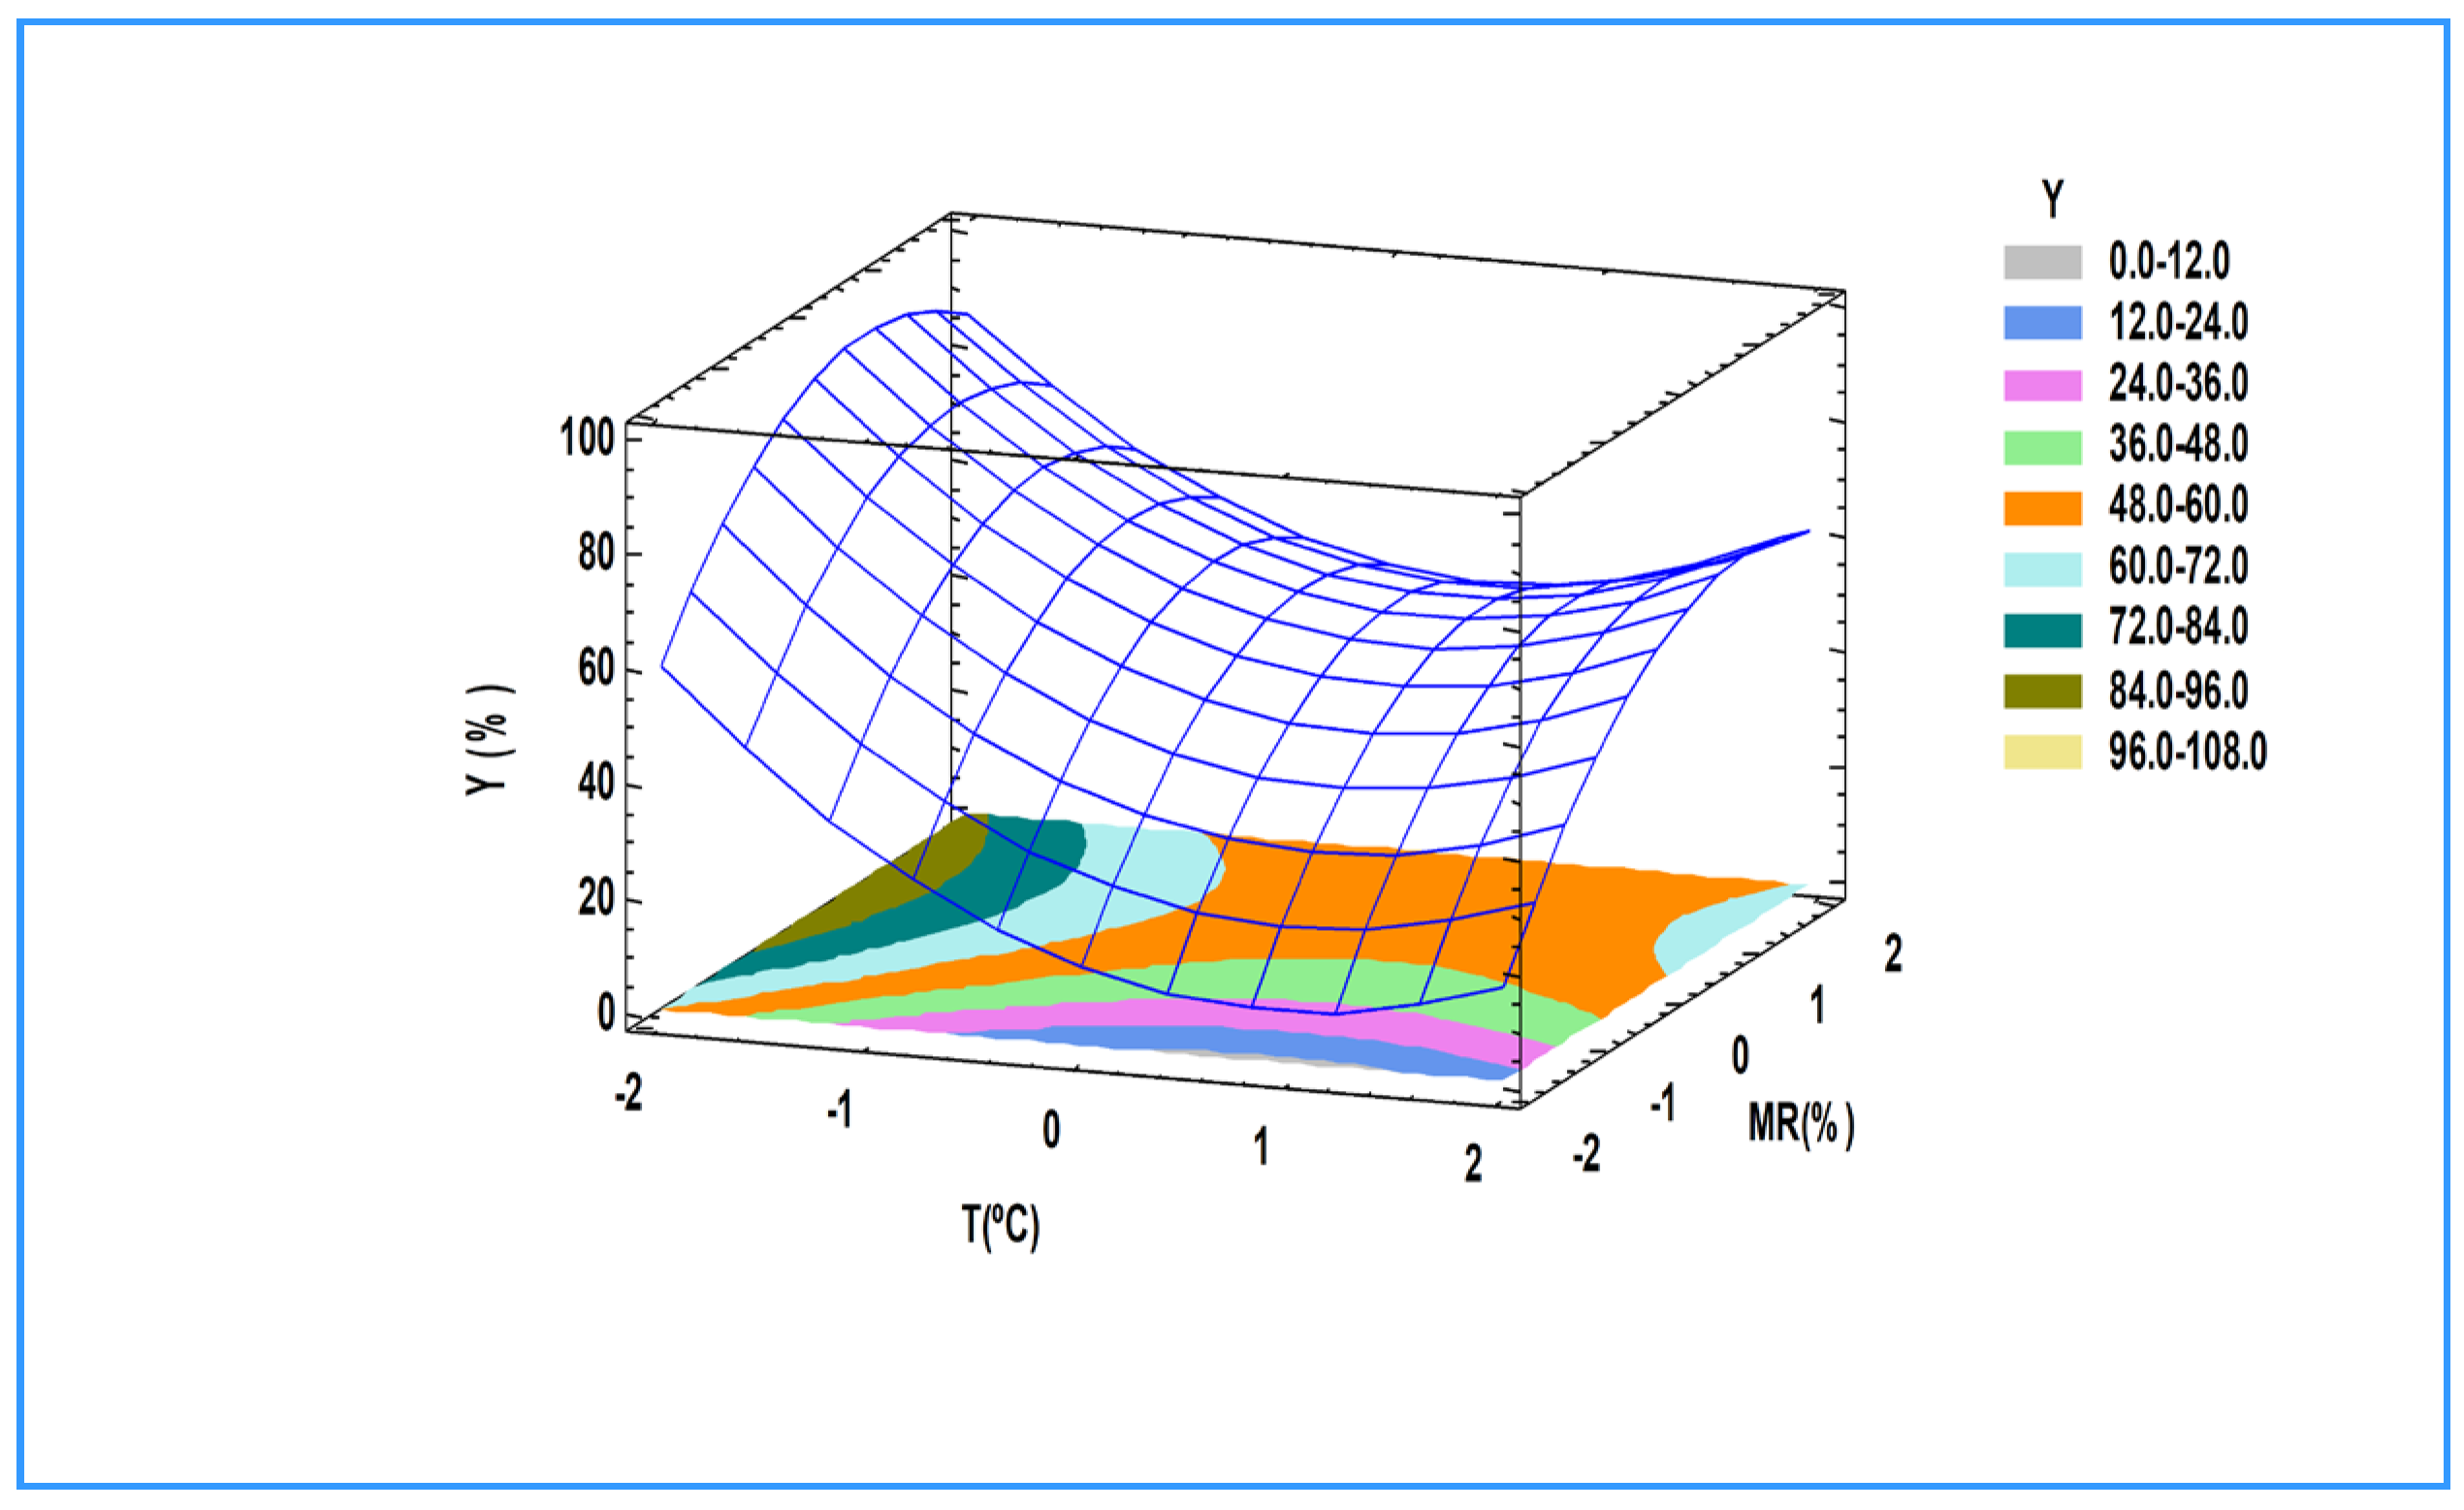
The synergistic effect of the binary ethanol-butanol system can be mechanistically explained by mass-transfer and steric factors. Butanol acts as a co-solvent, reducing the viscosity of the highly saturated coconut oil matrix and improving phase homogeneity. However, its longer alkyl chain introduces steric hindrance at the lipase active site compared to ethanol. The optimization via RSM successfully balanced these competing effects, achieving maximum conversion by regulating the nucleophilic strength of the medium without inducing alcohol-mediated enzyme deactivation.
As expected, the isolated C6–C12 fraction exhibited a freezing point of −30 °C, which does not meet the neat fuel constraint of −40 °C mandated by ASTM D7566. Consequently, this fraction functions strictly as a bio-based aviation blendstock. To comply with Jet A-1 specifications (−47 °C), the maximum blending ratio with conventional kerosene is restricted to 10–15% vol., ensuring that low-temperature operability and safety margins are not compromised during high-altitude flights.
We acknowledge that traditional Jet A-1 is predominantly composed of C9–C16 paraffins, naphthenes, and aromatics. The comparison of our C6–C12 ester fraction to the “aviation window” is justified strictly from a volatility and distillation profile perspective. The oxygen functionalities in the short-chain esters (C6–C8) increase polarity and intermolecular forces; structurally, this higher polarity shifts their boiling points upward, matching the evaporation profile of heavier C9–C11 pure hydrocarbons. Thus, the fraction mimics the distillation curve of fossil kerosene despite its distinct chemical nature and lower hydrocarbon backbone length.
4.2. Technical Validation and Strategic Suitability of the BJF Fraction
To validate the viability of the isolated BJF fraction (C6–C12) as a Sustainable Aviation Fuel (SAF) precursor, its physicochemical properties were benchmarked against the ASTM D7566 standard and Jet A-1 specifications. As summarized in
Table 9, the isolated fraction exhibits properties closely aligned with the requirements for synthetic blending components. Notably, the freezing point and kinematic viscosity—parameters intrinsically linked to the carbon-chain distribution—fall within the regulatory window for aviation turbine fuels. The successful isolation of this specific distillation cut confirms the efficacy of the fractional distillation strategy in filtering out high-molecular-weight species that would otherwise compromise cold-flow operability. The specialized nature of this light distillate, dominated by C6 (25%), C8 (52%), and C12 (14%) esters, aligns precisely with the “molecular window” required for aviation kerosene. The predominance of these medium-chain species imparts exceptional low-temperature fluidity, successfully mitigating the cold-flow limitations typically associated with long-chain saturated fatty acid esters. Beyond meeting standard specifications, this light fraction acts as a high-performance SAF blendstock; its integration into conventional Jet A-1 or synthetic paraffinic kerosenes (e.g., HEFA or Alcohol-to-Jet) not only increases the renewable carbon content but also enhances the fuel’s intrinsic lubricity—a known challenge in hydroprocessed synthetic fuels.
These results demonstrate that this cascading biorefinery approach transforms coconut oil into a versatile, modular feedstock by tailoring the molecular architecture through targeted fractionation. This methodology offers a scalable pathway to meet the stringent demands of the aviation sector while maximizing the value-added potential of each ester fraction, effectively bridging the gap between bio-derived esters and aviation-grade kerosene.
While key physical parameters such as density, viscosity, and cold-flow properties were optimized, a comprehensive aviation qualification requires further standardized testing under ASTM D4054 protocols. Future evaluations must encompass net heat of combustion, smoke point, and thermal oxidative stability (JFTOT). Consequently, the present data serve as a preliminary screening for oxygenated blendstocks rather than a formal certification of aviation-grade compliance.
Unlike immobilized catalysts, Eversa Transform 2.0 is a liquid enzyme formulation that partitions into the glycerol phase at the end of the reaction. Based on the optimized parameters of this study and analogous liquid-phase recycling architectures, the biocatalyst can be effectively recirculated for five consecutive operational cycles, maintaining over 80% of its initial relative transesterification yield. Beyond five cycles, mass-transfer losses and partial denaturation via alcohol contact reduce performance. This operational life translates to an estimated enzyme contribution of $38 USD per metric ton of processed ester matrix, aligning with industrial feasibility thresholds.
4.3. Strategic Implications for SAF Implementation
The implementation of the fractional distillation strategy to isolate a C6–C12 matrix represents a significant step in aligning coconut oil derivatives with the “molecular window” of aviation kerosene. While conventional fuels are predominantly hydrocarbon-based, the integration of FAEE/FABE offers a distinct strategic advantage through enhanced lubricity and oxygenated combustion properties. These medium-chain esters, characterized by lower molecular weights than standard biodiesel, improve atomization and volatility, effectively bridging the gap between fatty acid esters and traditional kerosene-type fuels.
4.4. Performance Benchmarks and Environmental Trade-Offs
A notable challenge in coconut-based SAF is the trade-off between energy density and cold-flow performance. While the net heat of combustion of oxygenated esters (~38–40 MJ/kg) is inherently lower than that of paraffinic fossil fuels (42–44 MJ/kg), this energetic penalty is strategically offset by three factors:
Emissions Profile: The oxygenated nature of the esters promotes more complete combustion, significantly reducing particulate matter (PM) and soot emissions.
Cascading Biorefinery Efficiency: The co-production of high-value C8–C14 industrial precursors enhances the techno-economic viability of the coconut-to-bio-jet pathway.
Synergistic Cold-Flow Modulation: The binary ethanol-butanol system provides a “molecular tailoring” effect. The butyl-branched chains disrupt the crystalline lattice of C12:0 and C14:0 components, inducing a substantial depression in both cloud and pour points. This structural reconfiguration validates the isolated fraction as a high-performance “drop-in” blendstock. By meeting ASTM D7566 requirements when blended with conventional Jet A-1, this process mitigates the dependence on synthetic pour point depressants (PPDs). Although the bulk ester mixture meets EN 14214 standards, the fractionated BJF represents a specialized product tailored for aviation. Future research will focus on full-scale turbine performance testing to validate the long-term integration of these enzymatic esters into modern aeronautical propulsion systems, reinforcing the potential of this modular biorefinery approach to scale renewable aviation solutions.