


Abstract
This work presents a comparative study of TiSiC and TiSiCN composite coatings deposited on stainless steel by reactive plasma spraying using mechanically activated powders. Microstructure, phase composition, and hardness were assessed by SEM/EDS, XRD, and Vickers indentation, while corrosion, erosion, and high-temperature tribological behavior were systematically evaluated. The TiCN + SiC + Si system forms a stable TiCxN1−x solid solution with amorphous Si3N4 grain-boundary phases, leading to densification and enhanced chemical stability. Compared with TiSiC, TiSiCN coatings exhibit higher hardness (2599 N/mm2, ≈324 HV), lower erosion loss (<1 mg), and stable friction coefficients (0.45–0.50 at 600 °C) due to protective oxide/nitride tribofilms. Electrochemical tests in 3.5 wt.% NaCl show a >6-fold reduction in corrosion rate (from 0.0506 to 0.008 mm·year−1) relative to bare steel. Overall, TiSiCN coatings deposited at 500–600 A provide an optimal balance of hardness, wear, and corrosion resistance, indicating strong potential for gas-turbine and power-generation components operating in aggressive environments.
1. Introduction
The development of multicomponent protective coatings with enhanced performance characteristics for operation in aggressive environments and at elevated temperatures is one of the key directions of modern materials science research [1]. Among the various types of coatings, those based on transition-metal nitrides and carbonitrides, such as TiN, TiCN, TiSiN, and TiSiCN, are of particular interest due to their high hardness, thermal stability, and oxidation resistance. Such coatings are widely applied in the oil and gas, power-generation, and aerospace industries to improve the wear and corrosion resistance of critical structural components [2,3,4,5].
TiSiCN coatings have attracted considerable attention due to their advantageous combination of properties, such as high microhardness, structural stability at temperatures up to 700 °C, and outstanding resistance to oxidation and corrosion. Studies by Ma et al. [6] demonstrated that the addition of silicon into carbonitride systems promotes the formation of an amorphous Si3N4 phase, which stabilizes the coating structure and reduces the coefficient of friction. According to Abraham et al. [7], nanocomposite TiSiCN coatings synthesized by plasma-enhanced chemical vapor deposition (PECVD) achieve ahardness values of about 35 GPa and exhibit stable frictional behavior at temperatures up to 600 °C. Endler et al. [8] further confirmed that the amorphous Si3N4 phase plays a key role in providing oxidation resistance in TiSiCN coatings deposited by CVD.
Despite these promising results, most published studies have focused on thin coatings (<5 μm) produced by physical vapor deposition (PVD) and chemical vapor deposition (CVD) methods [9,10]. While such coatings are effective under light mechanical loads, applications in high-temperature and aggressive environments, such as those encountered in power and gas turbine systems, require thicker coatings with high density and strong adhesion to the substrate. Reactive plasma spraying (RPS) [11] represents a promising technology in this regard, enabling the deposition of composite coatings with thicknesses up to 300 μm.
Research by Qin et al. [12] demonstrated that TiCN–Al2O3 composite coatings synthesized by RPS exhibited high microhardness and wear resistance at temperatures up to 700 °C. Zhang et al. [13] further reported that alloying carbonitride coatings with Cr and Mo promotes the formation of thermally stable phases, thereby enhancing their thermal stability and wear resistance. Similar findings were reported in subsequent studies by Wu et al. [14], where TiSiCN coatings prepared by magnetron sputtering exhibited high corrosion potential and low corrosion current in saline environments.
He Jining et al. [15] also demonstrated improved wear resistance of Ti–Si–C–Mo coatings after high-temperature heat treatment, highlighting the importance of studying the thermal stability of TiSiCN-based coatings. In addition, Wang et al. [16] reported a significant enhancement in the erosion resistance of thermally sprayed coatings due to the formation of protective oxide layers at temperatures above 600 °C.
A review of the current literature shows that TiSiCN coatings deposited by PVD and CVD methods are well studied with respect to their structure and tribological behavior at moderate temperatures. However, limited data are available on the performance of coatings synthesized by reactive plasma spraying, particularly under conditions of high temperatures, cyclic oxidation, and corrosion.
The aim of the present work is to conduct a comprehensive study of the corrosion resistance, erosion behavior, and high-temperature tribological properties of composite TiSiCN coatings produced by reactive plasma spraying. The results of this study will provide a scientific basis for recommending the application of TiSiCN coatings to protect components of power-generation and gas turbine systems from degradation under aggressive service conditions.
The novelty of this research lies in the first comprehensive comparative analysis of TiSiC and TiSiCN coatings synthesized by reactive plasma spraying using mechanically activated powders. Unlike previous studies focused on thin PVD/CVD layers, this work investigates the combined corrosion, erosion, and high-temperature tribological behavior of thick (26–51 µm) plasma-sprayed coatings, providing new insights into the relationship between composition, structure, and multifunctional performance.
2. Materials and Methods
2.1. Materials
High-purity titanium (Ti, 99.5%), silicon carbide (SiC, 99%), and titanium carbonitride (TiCN) powders were used as starting materials. Two powder systems were prepared for coating deposition: Ti + SiC and TiCN + SiC + Si. Fine titanium powder of grade PTOM-1 (≈30 µm), fine-grained SiC powder (≈20 µm, 99%), TiCN powder of 99.99% purity produced in Russia, and TiCN powder of 98% purity from China (used for comparative purposes) were employed. Silicon powder (99.5% purity, 15–45 µm, China) was also added to the TiCN + SiC + Si mixture.
The powders were mixed in fixed weight ratios to ensure reproducibility of coating composition: Ti–60 wt.% and SiC–40 wt.% for the Ti + SiC system; TiCN–60 wt.%, SiC–25 wt.%, and Si–15 wt.% for the TiCN + SiC + Si system. The stoichiometric ratios of the powder components were determined based on reaction equations and thermodynamic calculations previously reported in our earlier work [17].
Mechanical activation was performed in a high-energy ball mill Emax (Retsch, Haan, Germany) equipped with a water-cooling system. The ball-to-powder mass ratio was 10:1, the rotation speed 1100 rpm, and the milling duration 90 min, while the temperature was maintained between 23 °C and 27 °C. This process ensured effective dispersion, particle size reduction, and improved homogeneity due to high-energy impacts and intensive mixing. After mechanical activation, the powders exhibited finer particle size and rougher surfaces, promoting better melting and adhesion during reactive plasma spraying. The morphology of the activated powders was examined using an SEM3200 (CIQTEK Co., Ltd., Hefei, China) operated at an accelerating voltage of 15 kV.
Representative SEM images of the mechanically activated powder mixtures are shown in Figure 1. Figure 1 illustrates the morphology of the initial mechanically activated powders, not the wear-track morphology.
Figure 1.
SEM images of mechanically activated powder mixtures used for reactive plasma spraying: (a) Ti + SiC powder mixture; (b) TiCN + SiC + Si powder mixture.
Figure 1 shows the SEM micrographs of the mechanically activated powder mixtures used for reactive plasma spraying: (a) Ti + SiC and (b) TiCN + SiC + Si. The powders exhibit a relatively uniform particle size distribution and a roughened surface morphology typical of high-energy ball milling. The presence of micro- and submicron-sized agglomerates indicates efficient mechanical activation and partial adhesion between particles of different compositions. Elemental contrast in the backscattered electron (BSE) images confirms the homogeneous distribution of Ti, Si, C, and N within the mixtures, which is consistent with previous observations for Ti–Si–C–N systems prepared by mechanical activation [17].
Such morphological features are favorable for subsequent plasma spraying, as they enhance particle melting, interfacial bonding, and phase homogeneity in the resulting coatings.
The mechanically activated powders were subsequently used for coating deposition.
2.2. Deposition of TiSiCN Coatings by Reactive Plasma Spraying
TiSiCN coatings were deposited using a reactive plasma spraying system equipped with a custom-designed direct-flow plasma torch with a power of up to 40 kW. The spraying chamber pressure during deposition was maintained at 0.3–0.4 MPa. AISI 304 (12X18H9T) stainless steel samples measuring 20 × 20 × 3 mm were used as substrates, which were pre-cleaned in an ultrasonic bath with ethanol and acetone. The compositions of the powder mixtures are presented in Table 1. In this study, two separate systems—Ti/SiC and TiCN/SiC/Si—were considered. This division was chosen to enable a comparative analysis and to gain a deeper understanding of how the initial composition influences the processes of mechanical activation and phase formation.
Table 1.
Processing parameters of reactive plasma spraying for TiSiCN coatings.
In this study, three main parameters were varied: arc current (400, 500, and 600 A), hydrogen flow rate (1.3, 1.5, and 1.7 L/min), and argon flow rate (30, 35, and 40 L/min). All other parameters were kept constant: voltage 30 V, spraying distance 110 mm, nitrogen flow rate 40 L/min, chamber pressure 0.3–0.4 Pa, and powder feed rate 1.5–2.0 g/min.
The modification of powder compositions, namely Ti + SiC and TiCN + SiC + Si, aimed to promote the formation of multicomponent phases such as TiC, TiN, SiC, and SiCN, as supported by previous studies. Pogrebnjak et al. [18] demonstrated that the incorporation of Si and C into TiN leads to the formation of an amorphous–nanocrystalline structure with enhanced hardness and thermal stability. Similarly, Chen et al. [19] obtained dense, homogeneous Ti–Si–C–N coatings by optimizing the initial powder composition.
The selected arc current range (400–600 A) directly influences plasma energy and particle ionization, thereby affecting coating thickness, density, and adhesion. Zhou et al. [20] observed comparable morphological variations in TiN coatings when increasing current between 300 and 600 A. Gas flow rates were optimized according to their functional roles in the plasma process. Hydrogen (1.3–1.7 L/min) acted as a reducing agent, minimizing oxidation and improving homogeneity [21]. Argon (30–40 L/min) ensured stable plasma and efficient particle transport [22]. Nitrogen (40 L/min) served as the main reactive gas responsible for nitride phase formation (TiN, TiCN, SiCN), consistent with the observations of Duminica et al. [18,23,24,25].
The voltage (30 V) and torch–substrate distance (110 mm) were fixed to eliminate uncontrolled variations, as recommended by Wang et al. [26,27,28], who reported that deviations above 10 mm significantly reduce coating density. Before deposition, the AISI 304 substrates were polished and ultrasonically cleaned in acetone. During spraying, the powders were axially fed into the plasma jet using argon as the carrier gas. The reactive interactions of Ti + SiC and TiCN + SiC + Si components within the plasma flow led to the formation of complex Ti–Si–C–N phases, resulting in dense, well-adhered coatings. The schematic diagram and a detailed description of the spraying setup are provided in our previous publication [17].
2.3. Research Methods
The phase composition of the coatings was analyzed using X-ray diffraction (XRD) on an X’Pert PRO diffractometer (PANalytical, Netherlands) with monochromatized CuKα radiation (λ = 1.5406 Å), over a scanning range of 30–90° with a step size of 0.02° [26].
The surface morphology and cross-sectional microstructure of the coatings were examined using a scanning electron microscope, SEM3200 (CIQTEK Co., Ltd., Hefei, China), equipped with an energy-dispersive X-ray spectrometer (EDS), XFlash 730M-300 (Bruker, Germany). The accelerating voltage was 15 kV, and both secondary electron (SE) and backscattered electron (BSE) detectors were used to obtain detailed images. Prior to analysis, the samples were mounted in epoxy resin, polished, and chemically etched in a 4% HNO3–ethanol solution for 30 s. It should be noted that the EDS method is not sufficiently accurate for quantitative determination of light elements such as C and N; in this study, it was applied only for qualitative confirmation of their distribution. It should be noted that energy-dispersive X-ray spectroscopy (EDS) provides limited accuracy for light elements such as carbon and nitrogen and is sensitive to surface topography and measurement conditions. Therefore, all EDS results in this work are interpreted as semi-quantitative and are used to evaluate the relative elemental distribution rather than to determine the exact stoichiometry of the coatings.
High-temperature tribological tests were performed using a TNT-S-AX0000 tribometer (Anton Paar GmbH, Graz, Austria) in a ball-on-disk configuration under dry sliding conditions. The counterpart material was an Al2O3 ball with a diameter of 6 mm. The tests were conducted at 400 °C, 550 °C, and 700 °C with a normal load of 5 N, a sliding speed of 0.1 m/s, and a total duration of 90 min. The friction coefficient was continuously recorded, and the wear track morphology was analyzed after testing by SEM to determine wear mechanisms.
Erosion resistance was evaluated according to ASTM G76-04 using Al2O3 particles (50 µm) as the erodent at an impact angle of 90° and a particle velocity of 50 m/s. The test duration was 10 min, and the mass loss of the coatings was measured with a precision balance (±0.1 mg) before and after testing. The erosion rate (E) was calculated using the equation:
where Δm is the mass loss (g), A is the exposed area (cm2), and t is the test time (min).
Electrochemical corrosion tests were carried out using potentiodynamic polarization in 3.5% NaCl solution, with a scan rate of 0.5 mV/s over a potential range of −0.8 V to +0.8 V.
For all samples, the corrosion current density was calculated using the geometric exposed area of 1.0 cm2. Because the plasma-sprayed coatings possess an increased surface roughness, the obtained current densities and corrosion rates should be considered as apparent values, which may slightly underestimate the true local current density. Each polarization test was performed on three independently coated samples (n = 3), and the electrochemical parameters are presented as mean ± standard deviation.
The cyclic oxidation behavior of the TiSiCN coatings was studied in air at 700 °C for a total duration of 30 h, with intermediate weighing every 5 h to monitor mass gain. The oxidation kinetics were evaluated from the Δm–t dependence (mass gain versus time), which was used to assess the thermal stability of the coatings under high-temperature oxidative conditions.
Microhardness measurements were performed using a FISCHERSCOPE HM2000S nanoindenter (Filmetrics, Milpitas, CA, USA) in accordance with DIN EN ISO 14577-1 (ISO 14577-1:2015. Metallic materials—Instrumented indentation test for hardness and materials parameters—Part 1: Test method. ISO: Geneva, Switzerland, 2015.). A Vickers-type diamond indenter with an apex angle of 136° was used. The peak load during indentation was set to 300 mN, with a loading time of 20 s and a holding segment of 5 s at maximum load to account for creep effects. Under these conditions, the indentation depth was 2.0–2.5 μm, while the coating thickness measured from cross-sectional micrographs was 35–40 μm. Thus, the penetration depth did not exceed 10% of the coating thickness, which ensures the absence of substrate influence and guarantees the reliability of hardness measurements for thin coatings [27]. Data processing was carried out using the WIN-HCU software package (Version 7.1).
3. Results and Discussion
3.1. XRD Analysis
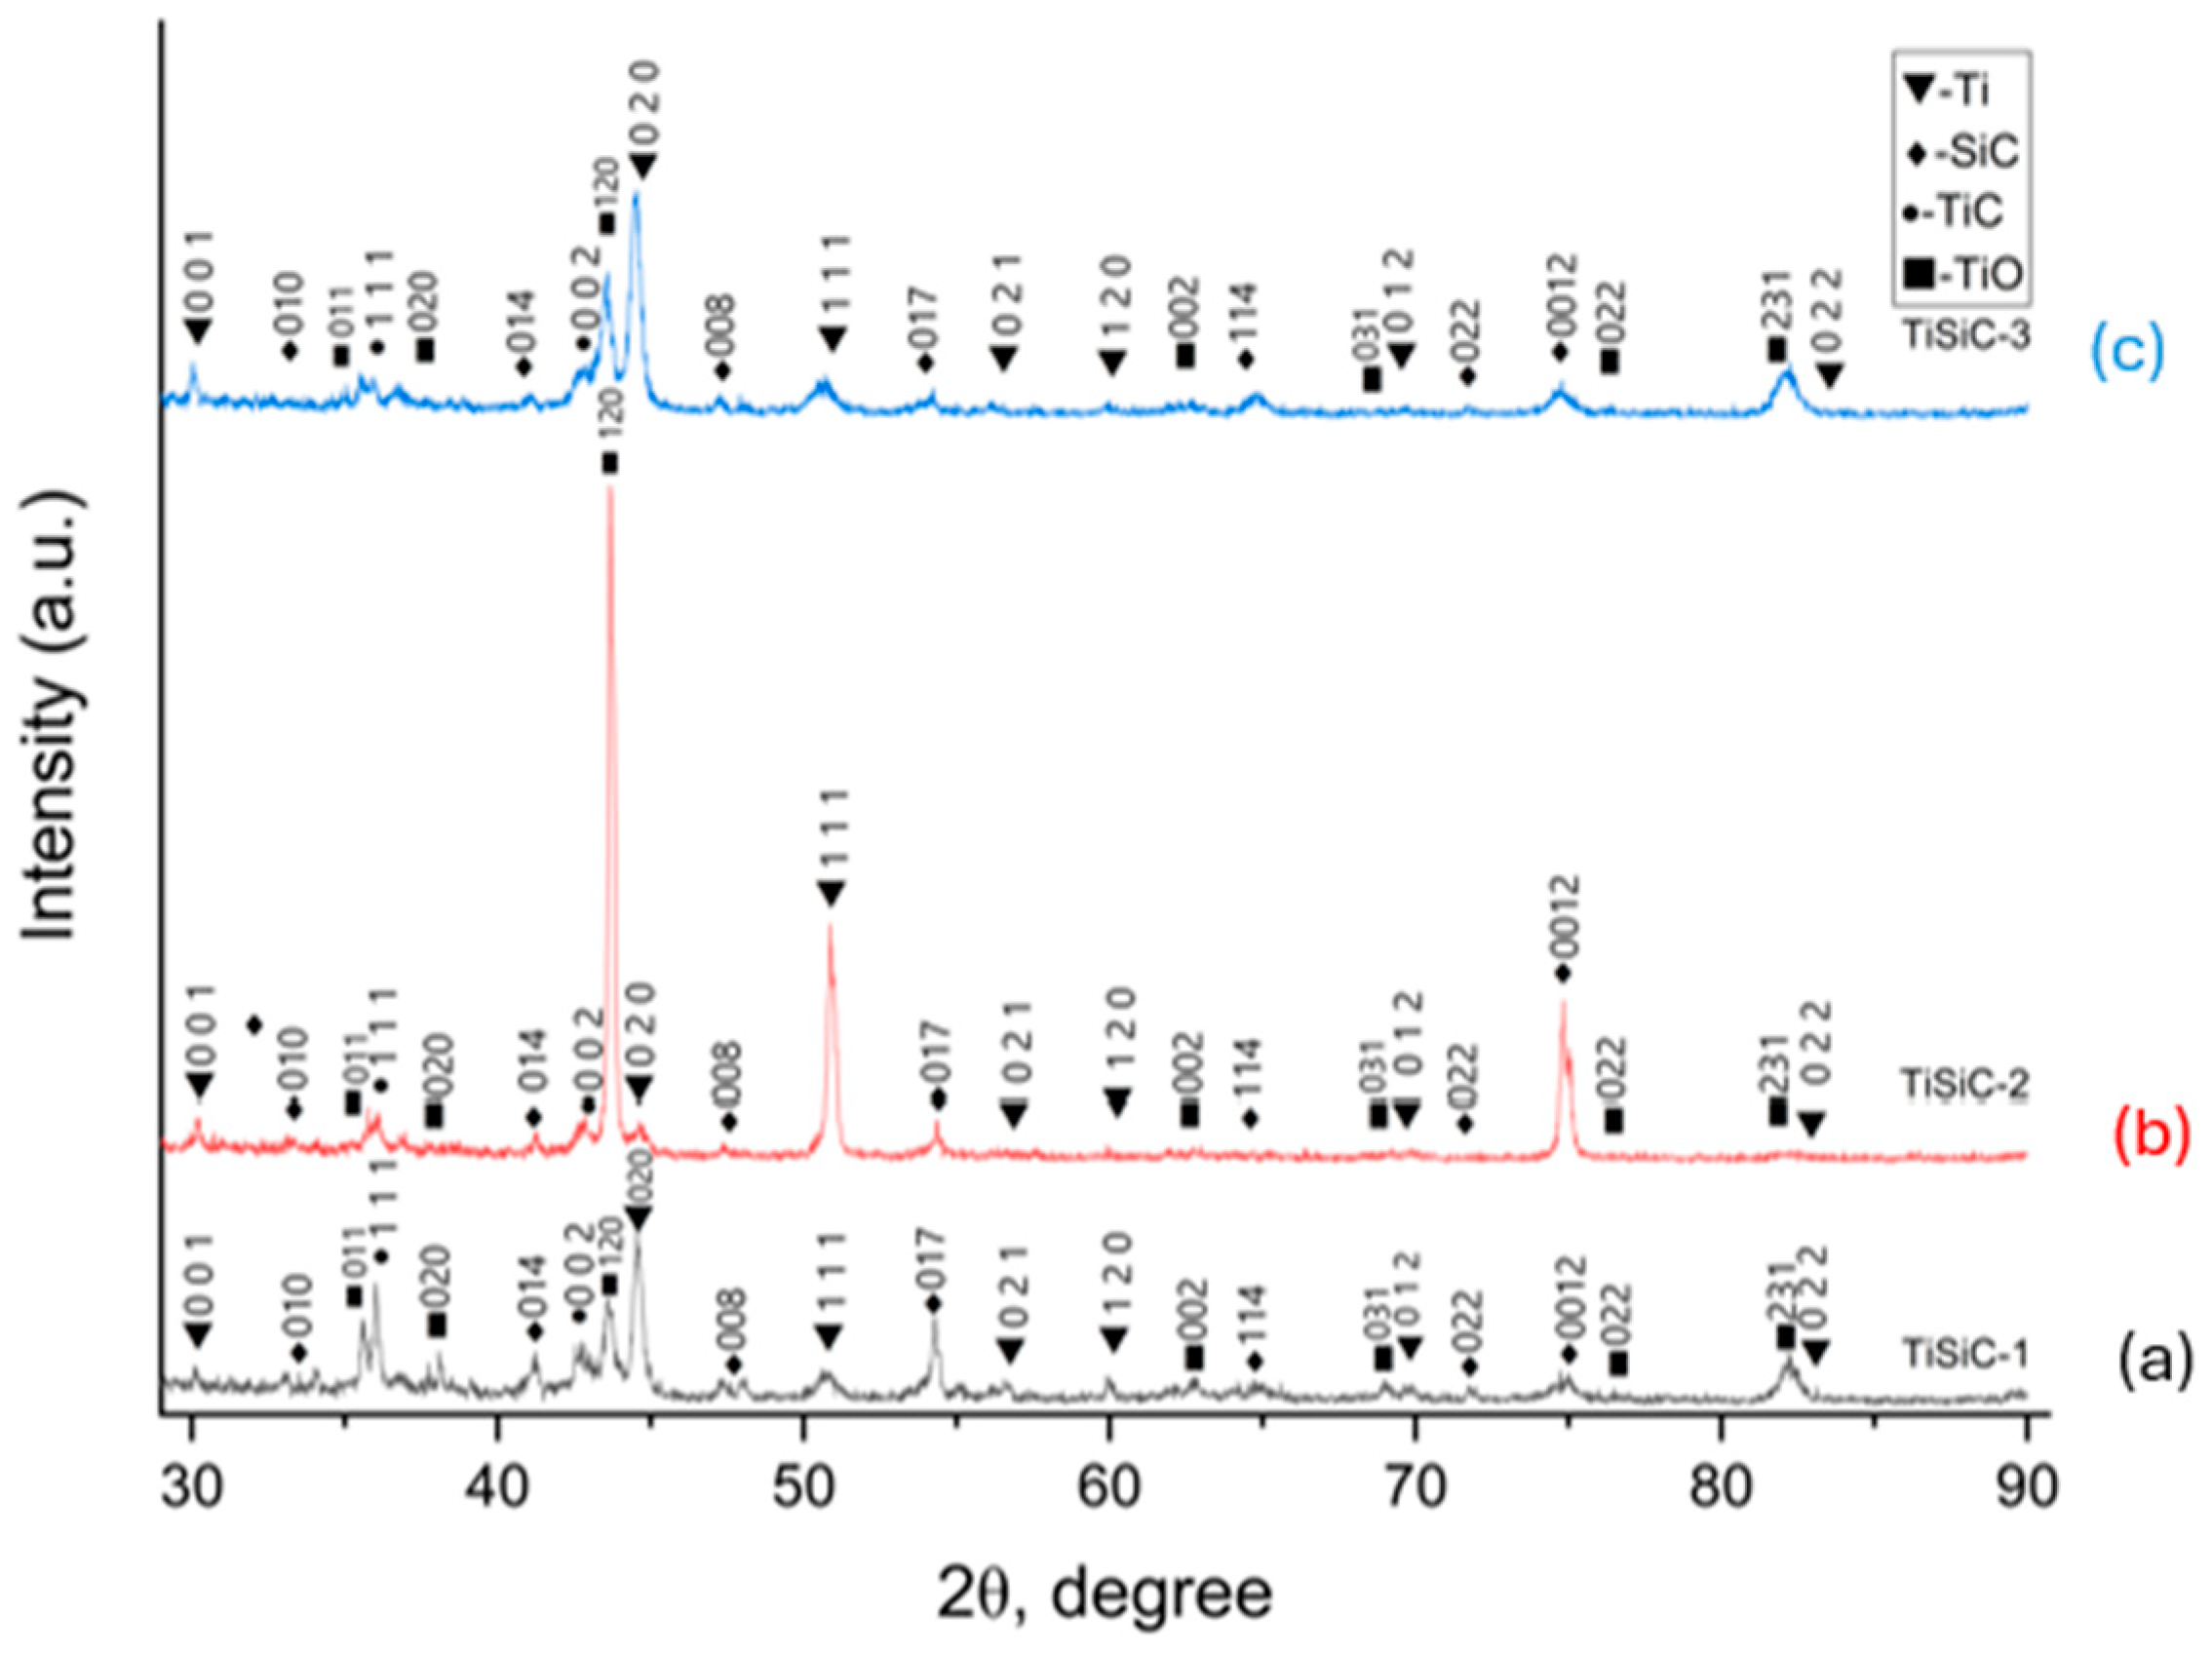
Figure 2 presents the X-ray diffraction (XRD) patterns of the Ti + SiC coatings obtained at different arc currents (400–600 A).
Figure 2.
X-ray diffraction patterns of TiSiC coatings deposited at different arc currents: (a) TiSiC-1, (b) TiSiC-2, (c) TiSiC-3.
The XRD patterns (Figure 2) show that the dominant reflections correspond to metallic titanium (Ti) and titanium monoxide (TiO), while the TiC phase is present only as weak peaks at 2Ɵ ≈ 36.2° and 42.1°. This indicates that carbide formation is incomplete under the selected plasma spraying conditions. As the arc current increases from 400 A to 600 A, the intensity of the TiC peaks slightly rises, suggesting partial transformation of Ti and TiO into TiC due to enhanced reaction between Ti and SiC at higher temperatures.
The reflections marked as Ti correspond to the hexagonal α-Ti phase (space group P63/mmc, PDF#44-1294), with characteristic peaks near 35.1°, 38.4°, and 40.2°, consistent with standard ICDD data.
Overall, all Ti + SiC coatings exhibit a multiphase composition dominated by Ti and TiO, with minor TiC and SiC phases. The coating deposited at 500 A (TiSiC-2) shows the best structural uniformity and reduced oxide content, indicating more favorable plasma parameters for the Ti–Si–C reaction system.
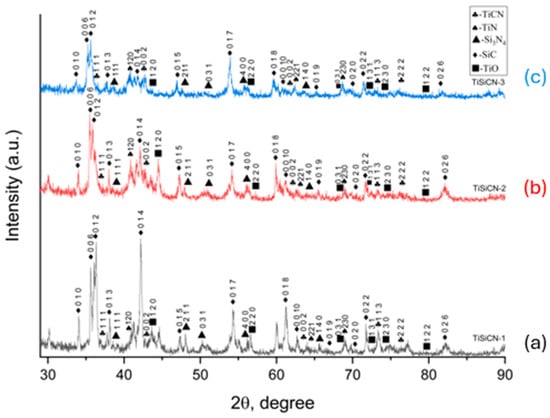
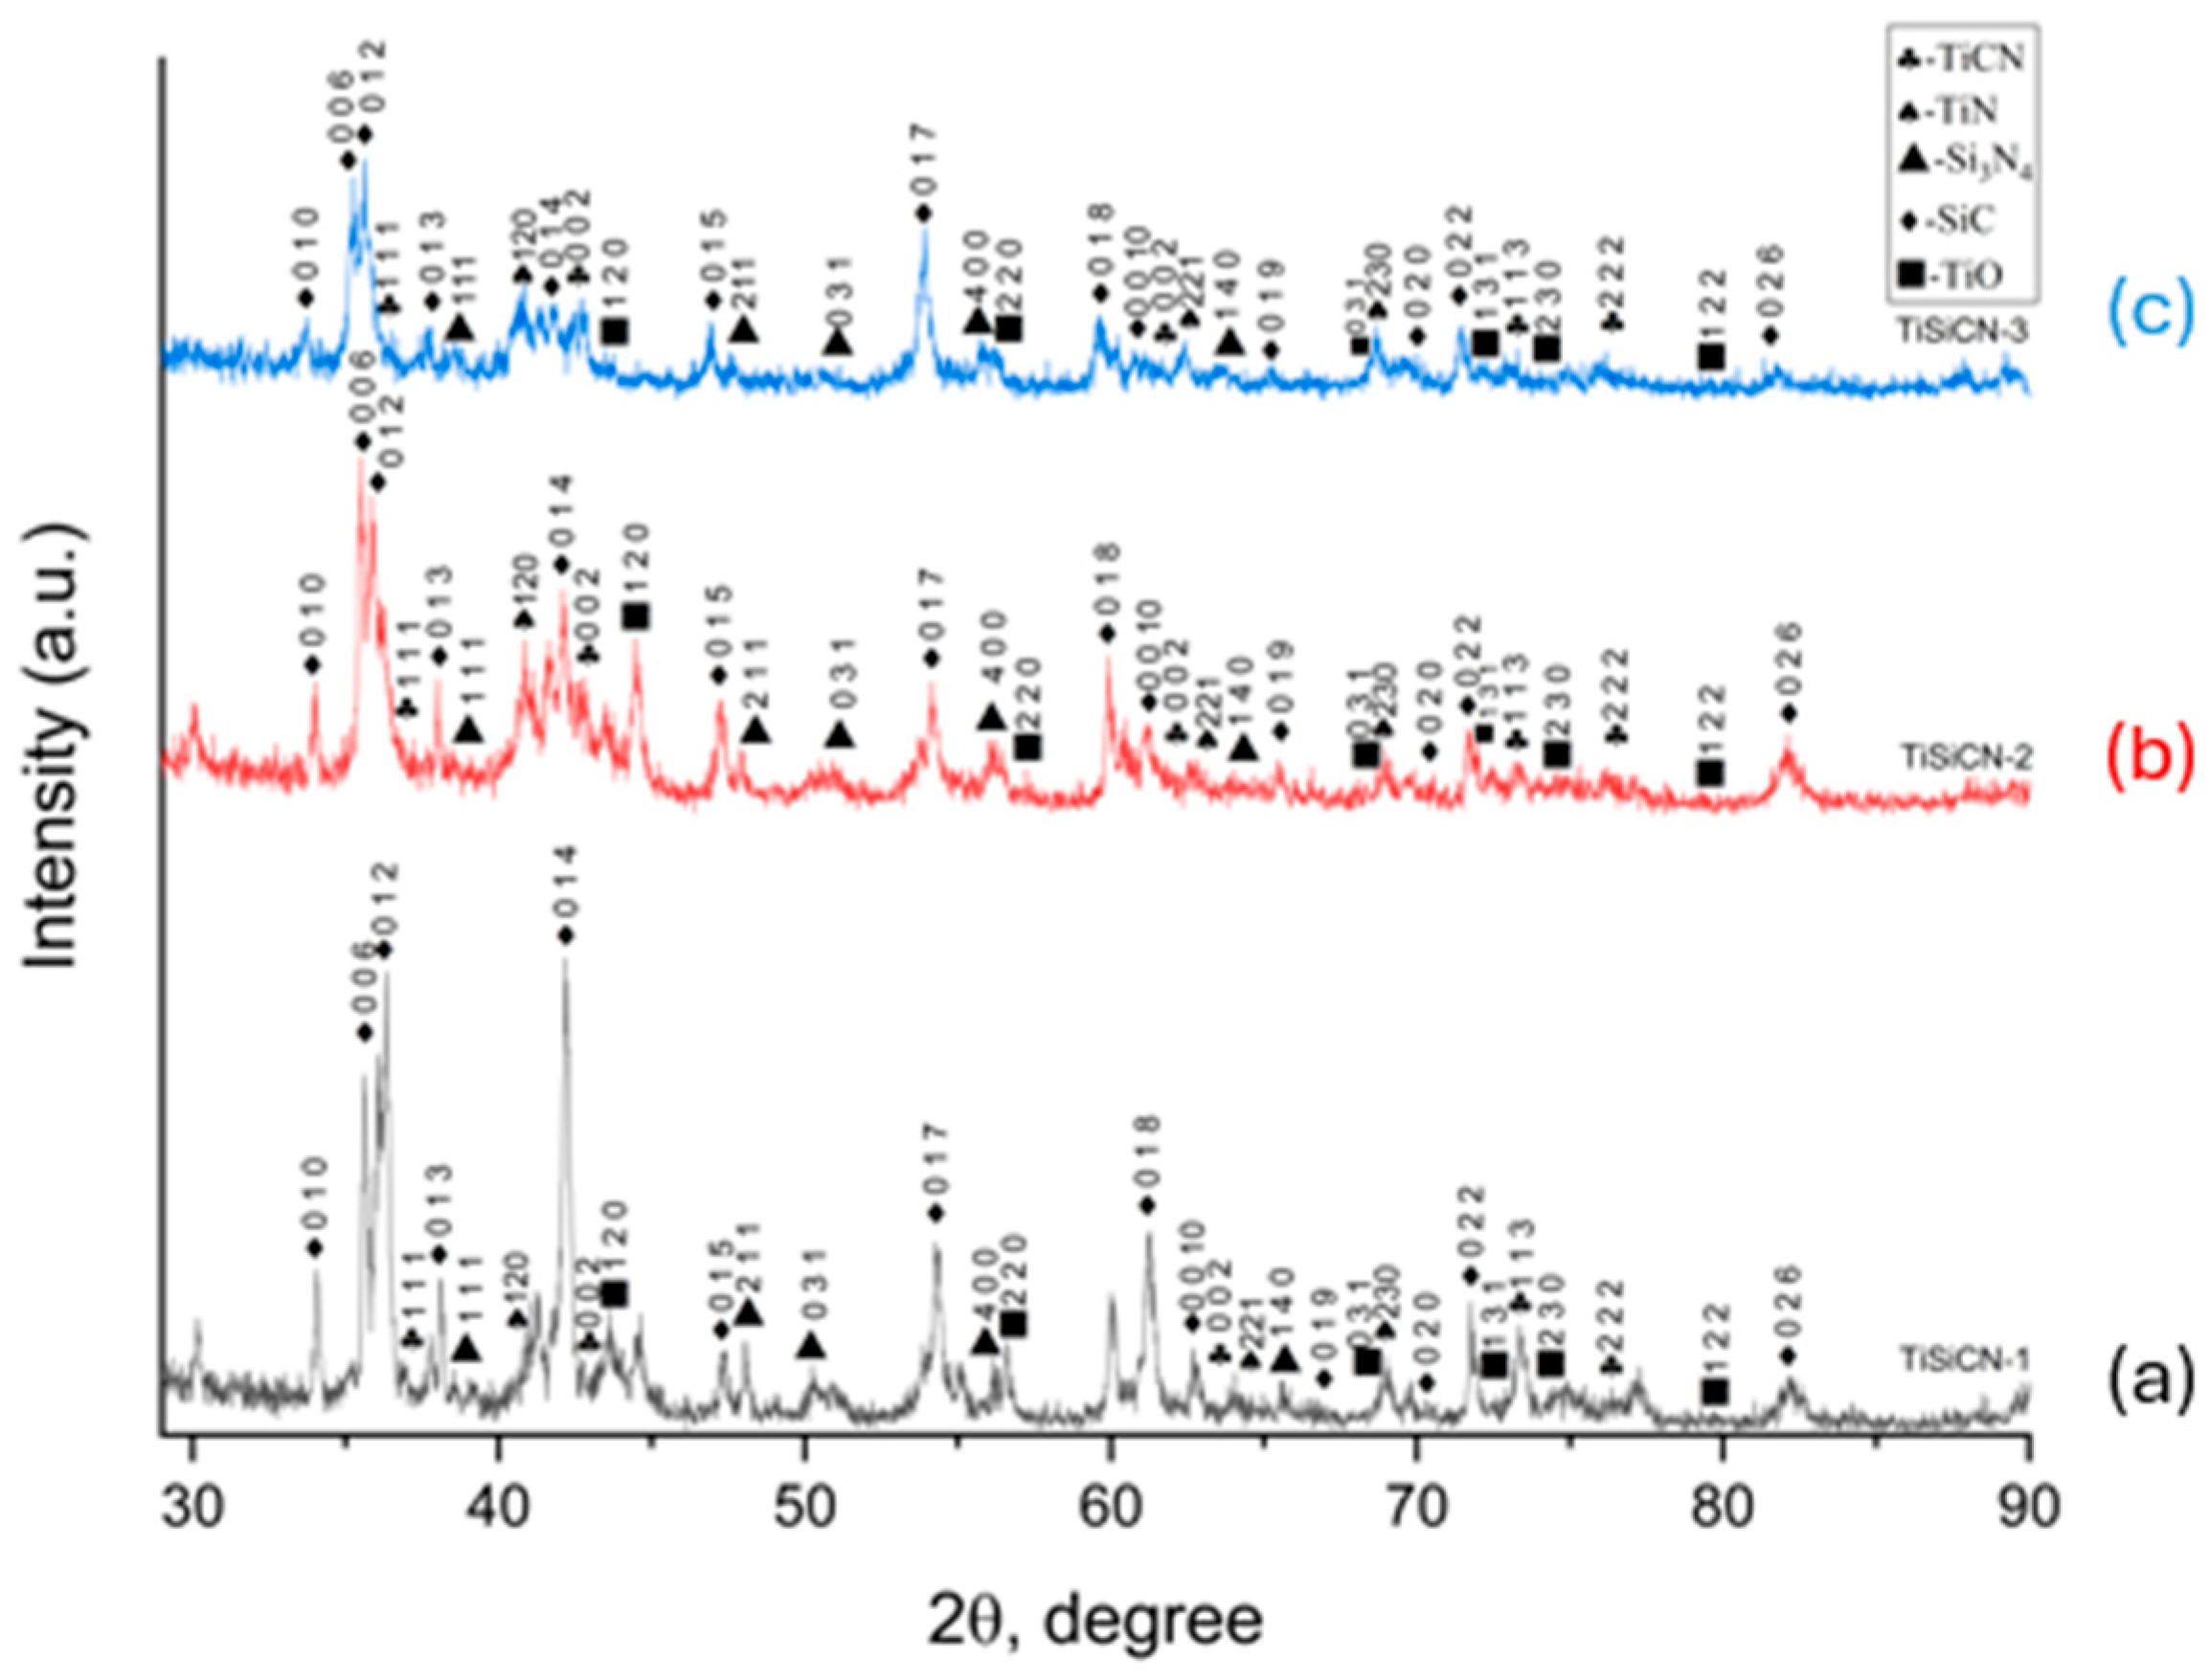
Figure 3 presents the X-ray diffraction (XRD) patterns of the TiCN + SiC + Si coatings deposited at arc currents of 400, 500, and 600 A.
Figure 3.
X-ray diffraction patterns of TiSiCN coatings deposited at different arc currents: (a) TiSiCN-1 (400 A), (b) TiSiCN-2 (500 A), (c) TiSiCN-3 (600 A).
The diffraction peaks correspond primarily to the Ti(C,N) solid-solution phase (Fm-3 m) with characteristic reflections at 2θ ≈ 36.0°, 41.7°, 60.4°, and 71.8°, confirming nitrogen incorporation into the TiC lattice. Additional reflections associated with TiN (43.6°, 63.6°) and Si3N4 (34.2°, 44.2°, 57.6°) are also detected, indicating partial nitridation of titanium and silicon during reactive plasma spraying. Weak signals of SiC (35.6°, 75.3°) and TiO2 (27.4°, 54.3°) correspond to secondary phases formed due to slight oxidation in the plasma jet environment. With increasing arc current from 400 A to 600 A, the Ti(C,N) peaks become sharper and more intense, suggesting improved crystallinity and solid-solution formation. The shift in the main Ti(C,N) reflections toward higher diffraction angles indicates lattice contraction resulting from substitution of larger carbon atoms with smaller nitrogen atoms. Such a trend is consistent with the results of Pogrebnjak et al. [18] and Chen et al. [19], who demonstrated that Si and N additions to TiN/TiC systems promote the formation of amorphous-nanocrystalline TiSiCN structures with enhanced hardness and thermal stability. The presence of Si3N4 and SiC phases agrees with findings by Duminica et al. [18,23,24,25,26], confirming that silicon acts as a glass-forming element, leading to partial amorphization of grain boundaries and suppression of Ti(C,N) grain growth. Weak TiO2 peaks, typical for plasma-sprayed coatings, are attributed to residual oxidation at high temperature, as also reported by Zhou et al. [20] and Gkomoza, P. et al. [21] for reactive plasma and arc processes.
Among all samples, the TiSiCN-3 coating (600 A) exhibits the most pronounced and well-defined Ti(C,N) and Si3N4 reflections with minimal oxide traces, indicating the formation of a dense nanocomposite structure consisting of Ti(C,N) crystallites embedded in an amorphous Si3N4/SiC matrix. This microstructural configuration ensures high hardness, thermal stability, and oxidation resistance—in full agreement with the nanocomposite model proposed by [26] and later confirmed in TiSiCN systems by [27].
3.2. Surface Morphology and Microstructure
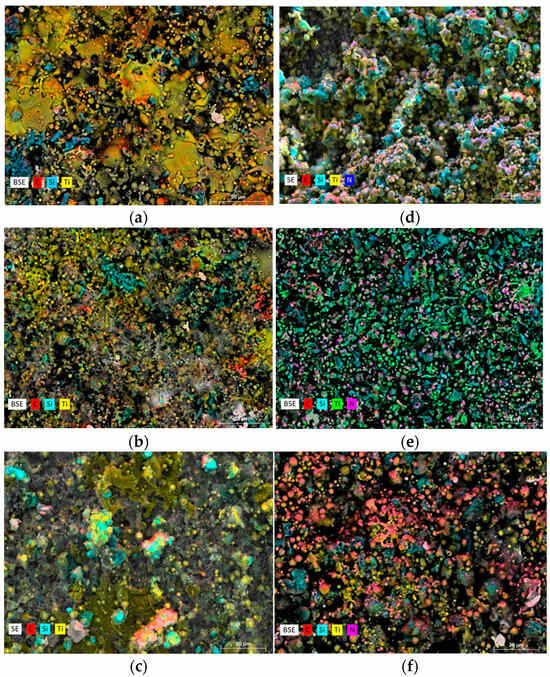
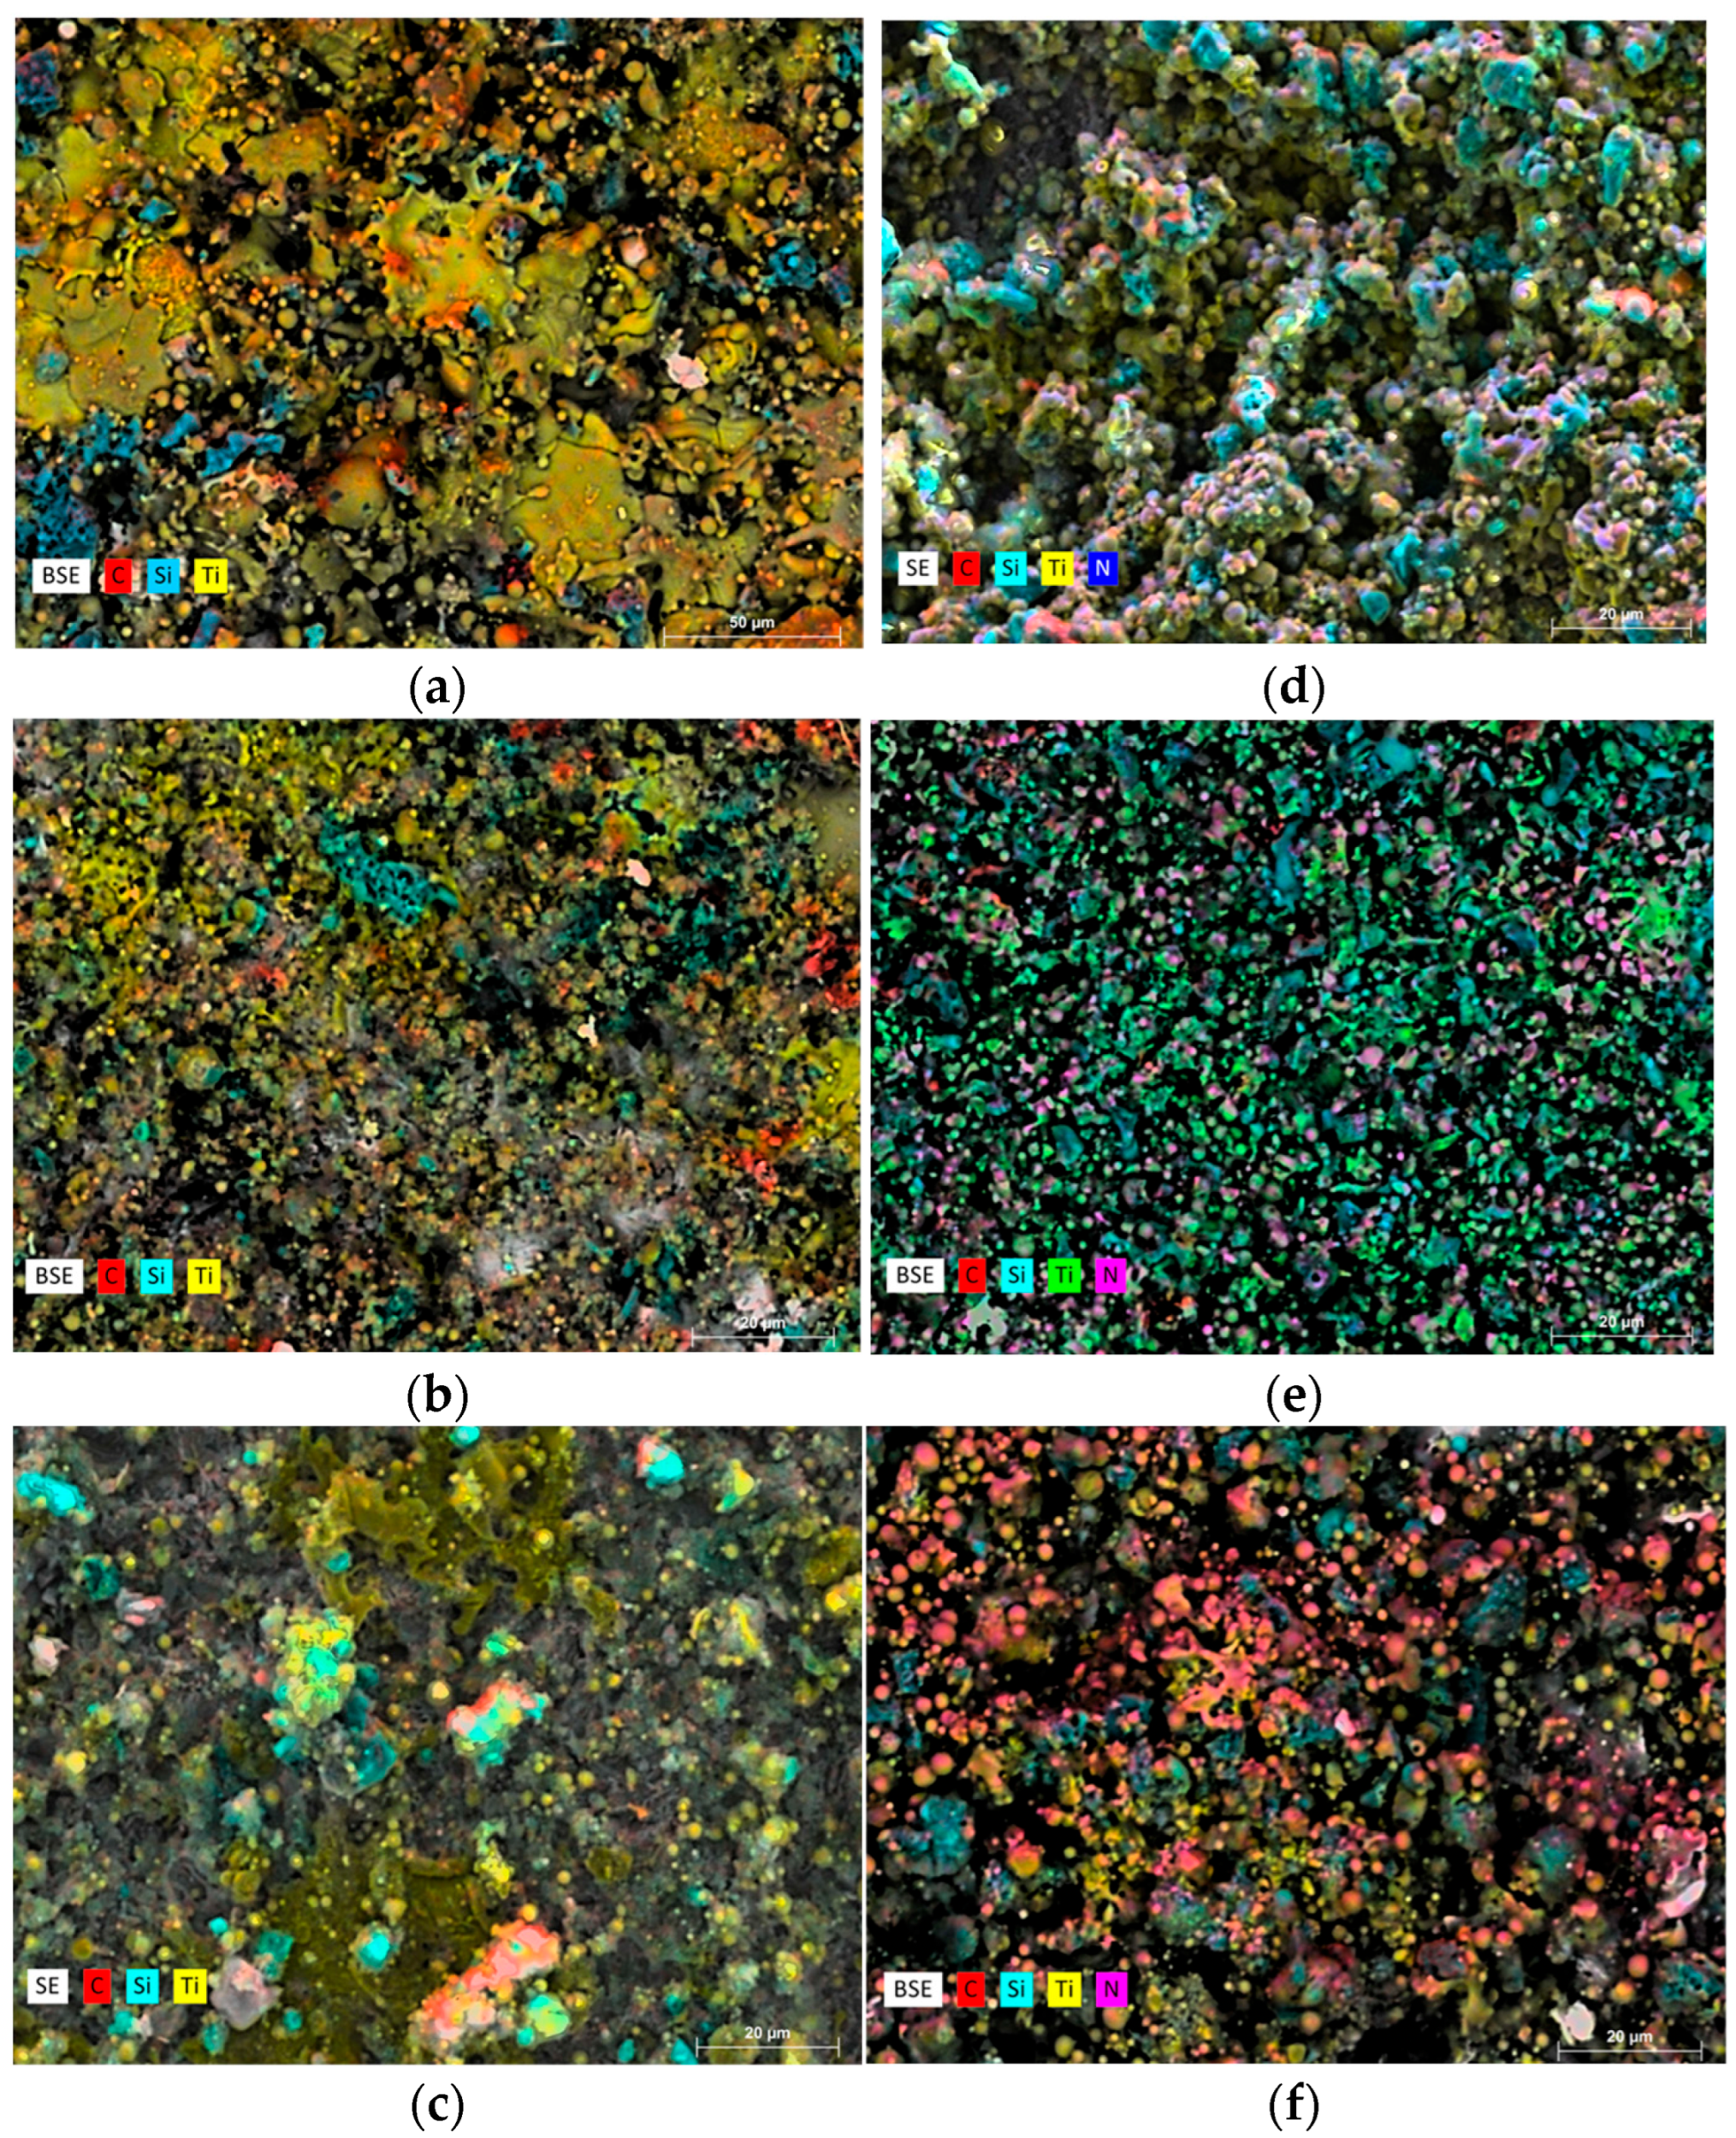
After the phase composition analysis by XRD, a detailed microstructural investigation was performed using SEM combined with EDS. Representative SEM micrographs and elemental distribution maps for all six coatings are presented in Figure 4. The TiSiC series (a–c) shows relatively homogeneous distribution of Ti, Si and C, while in the TiSiCN series (d–f) the elemental maps also reveal nitrogen incorporation, although its detection is limited by the sensitivity of EDS. These observations are in agreement with the quantitative EDS results (Table 2) and confirm the influence of the initial powder composition and deposition current on the elemental uniformity of the coatings.
Figure 4.
SEM micrographs and EDS elemental maps of the coatings: (a) TiSiC-1, (b) TiSiC-2, (c) TiSiC-3, (d) TiSiCN-1, (e) TiSiCN-2, (f) TiSiCN-3.
Table 2.
Quantitative EDS composition of TiSiC and TiSiCN coatings (at.%).
Among all coatings, TiSiC-2 and TiSiCN-3 show the most uniform elemental distribution, dense microstructure, and minimal porosity, which agrees with their improved mechanical characteristics. This trend is consistent with the observations of Pogrebnjak et al. [18] and Fouad, O. A., et al. [23], who reported that Si and N additions promote structural homogenization and refinement of Ti(C,N)-based coatings. For a more detailed comparison, the quantitative EDS results for all six samples are summarized in Table 2.
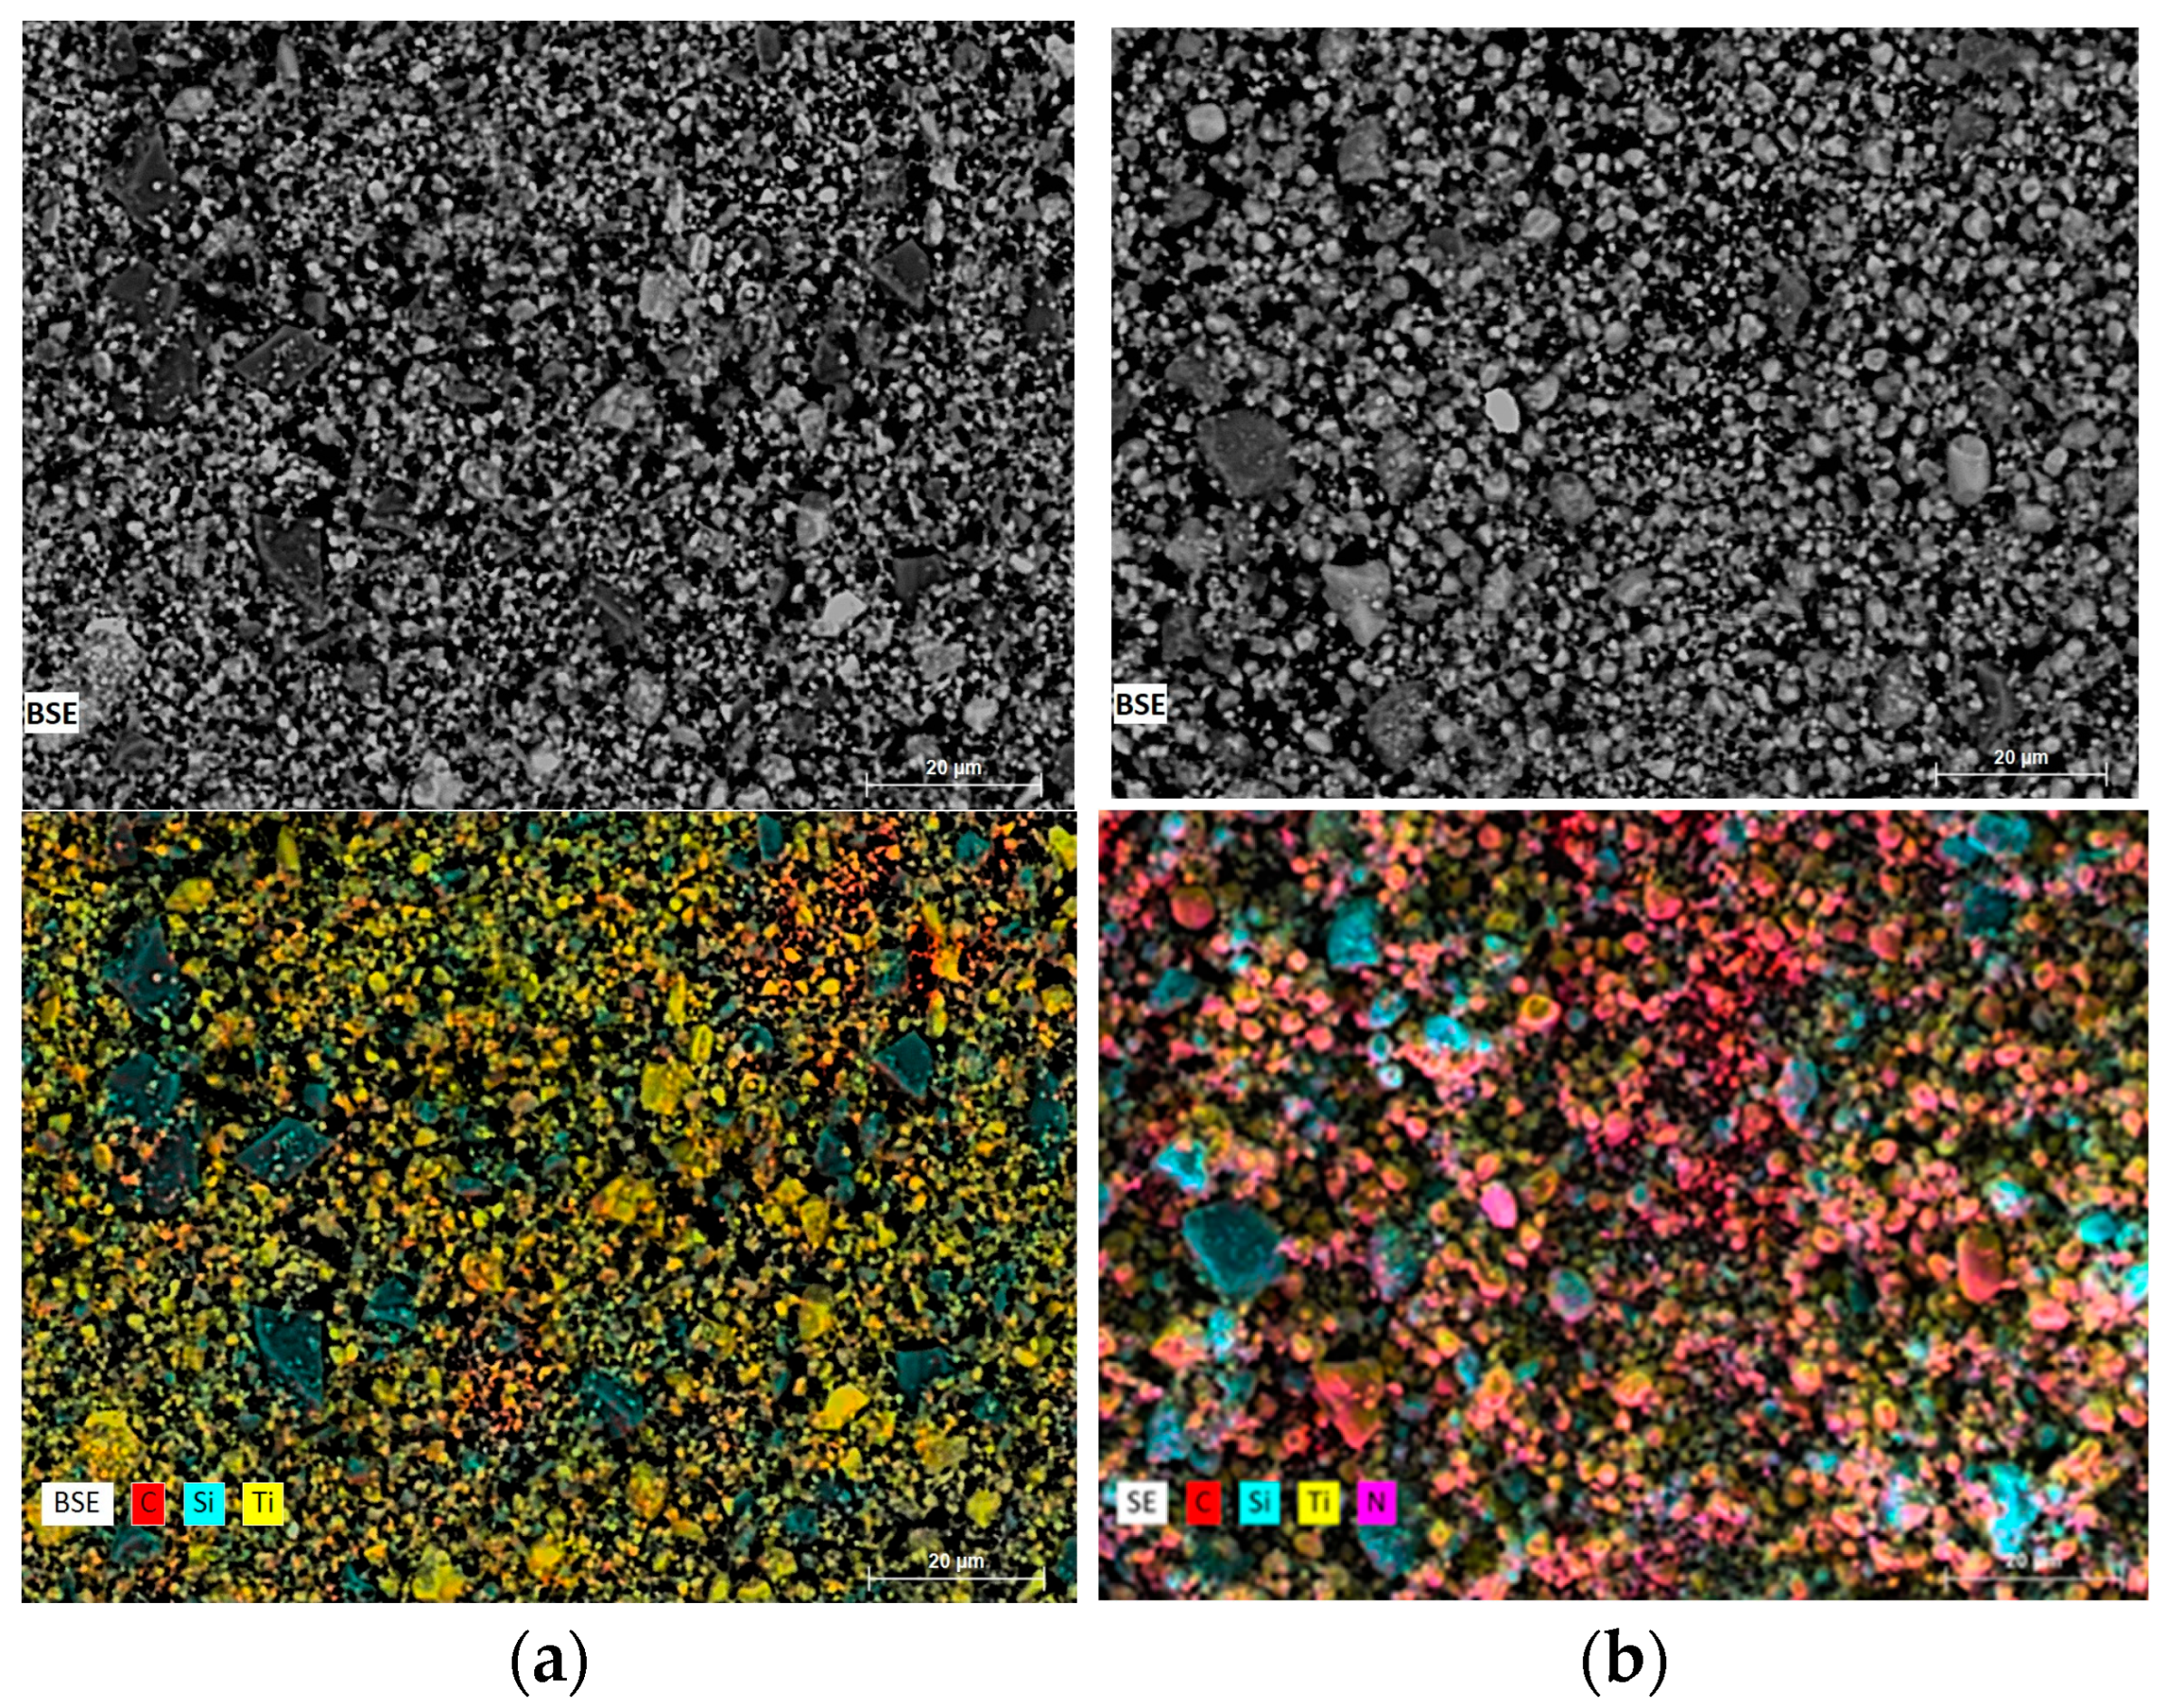
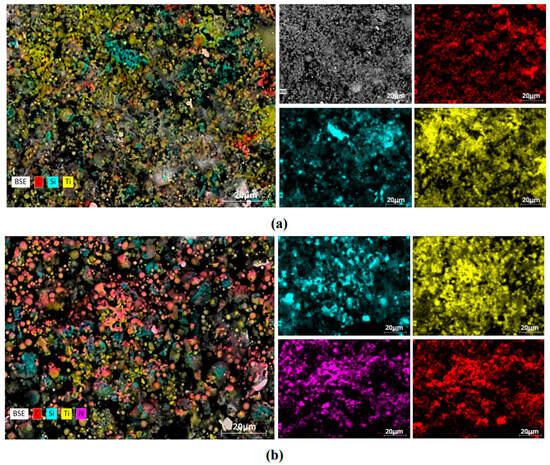
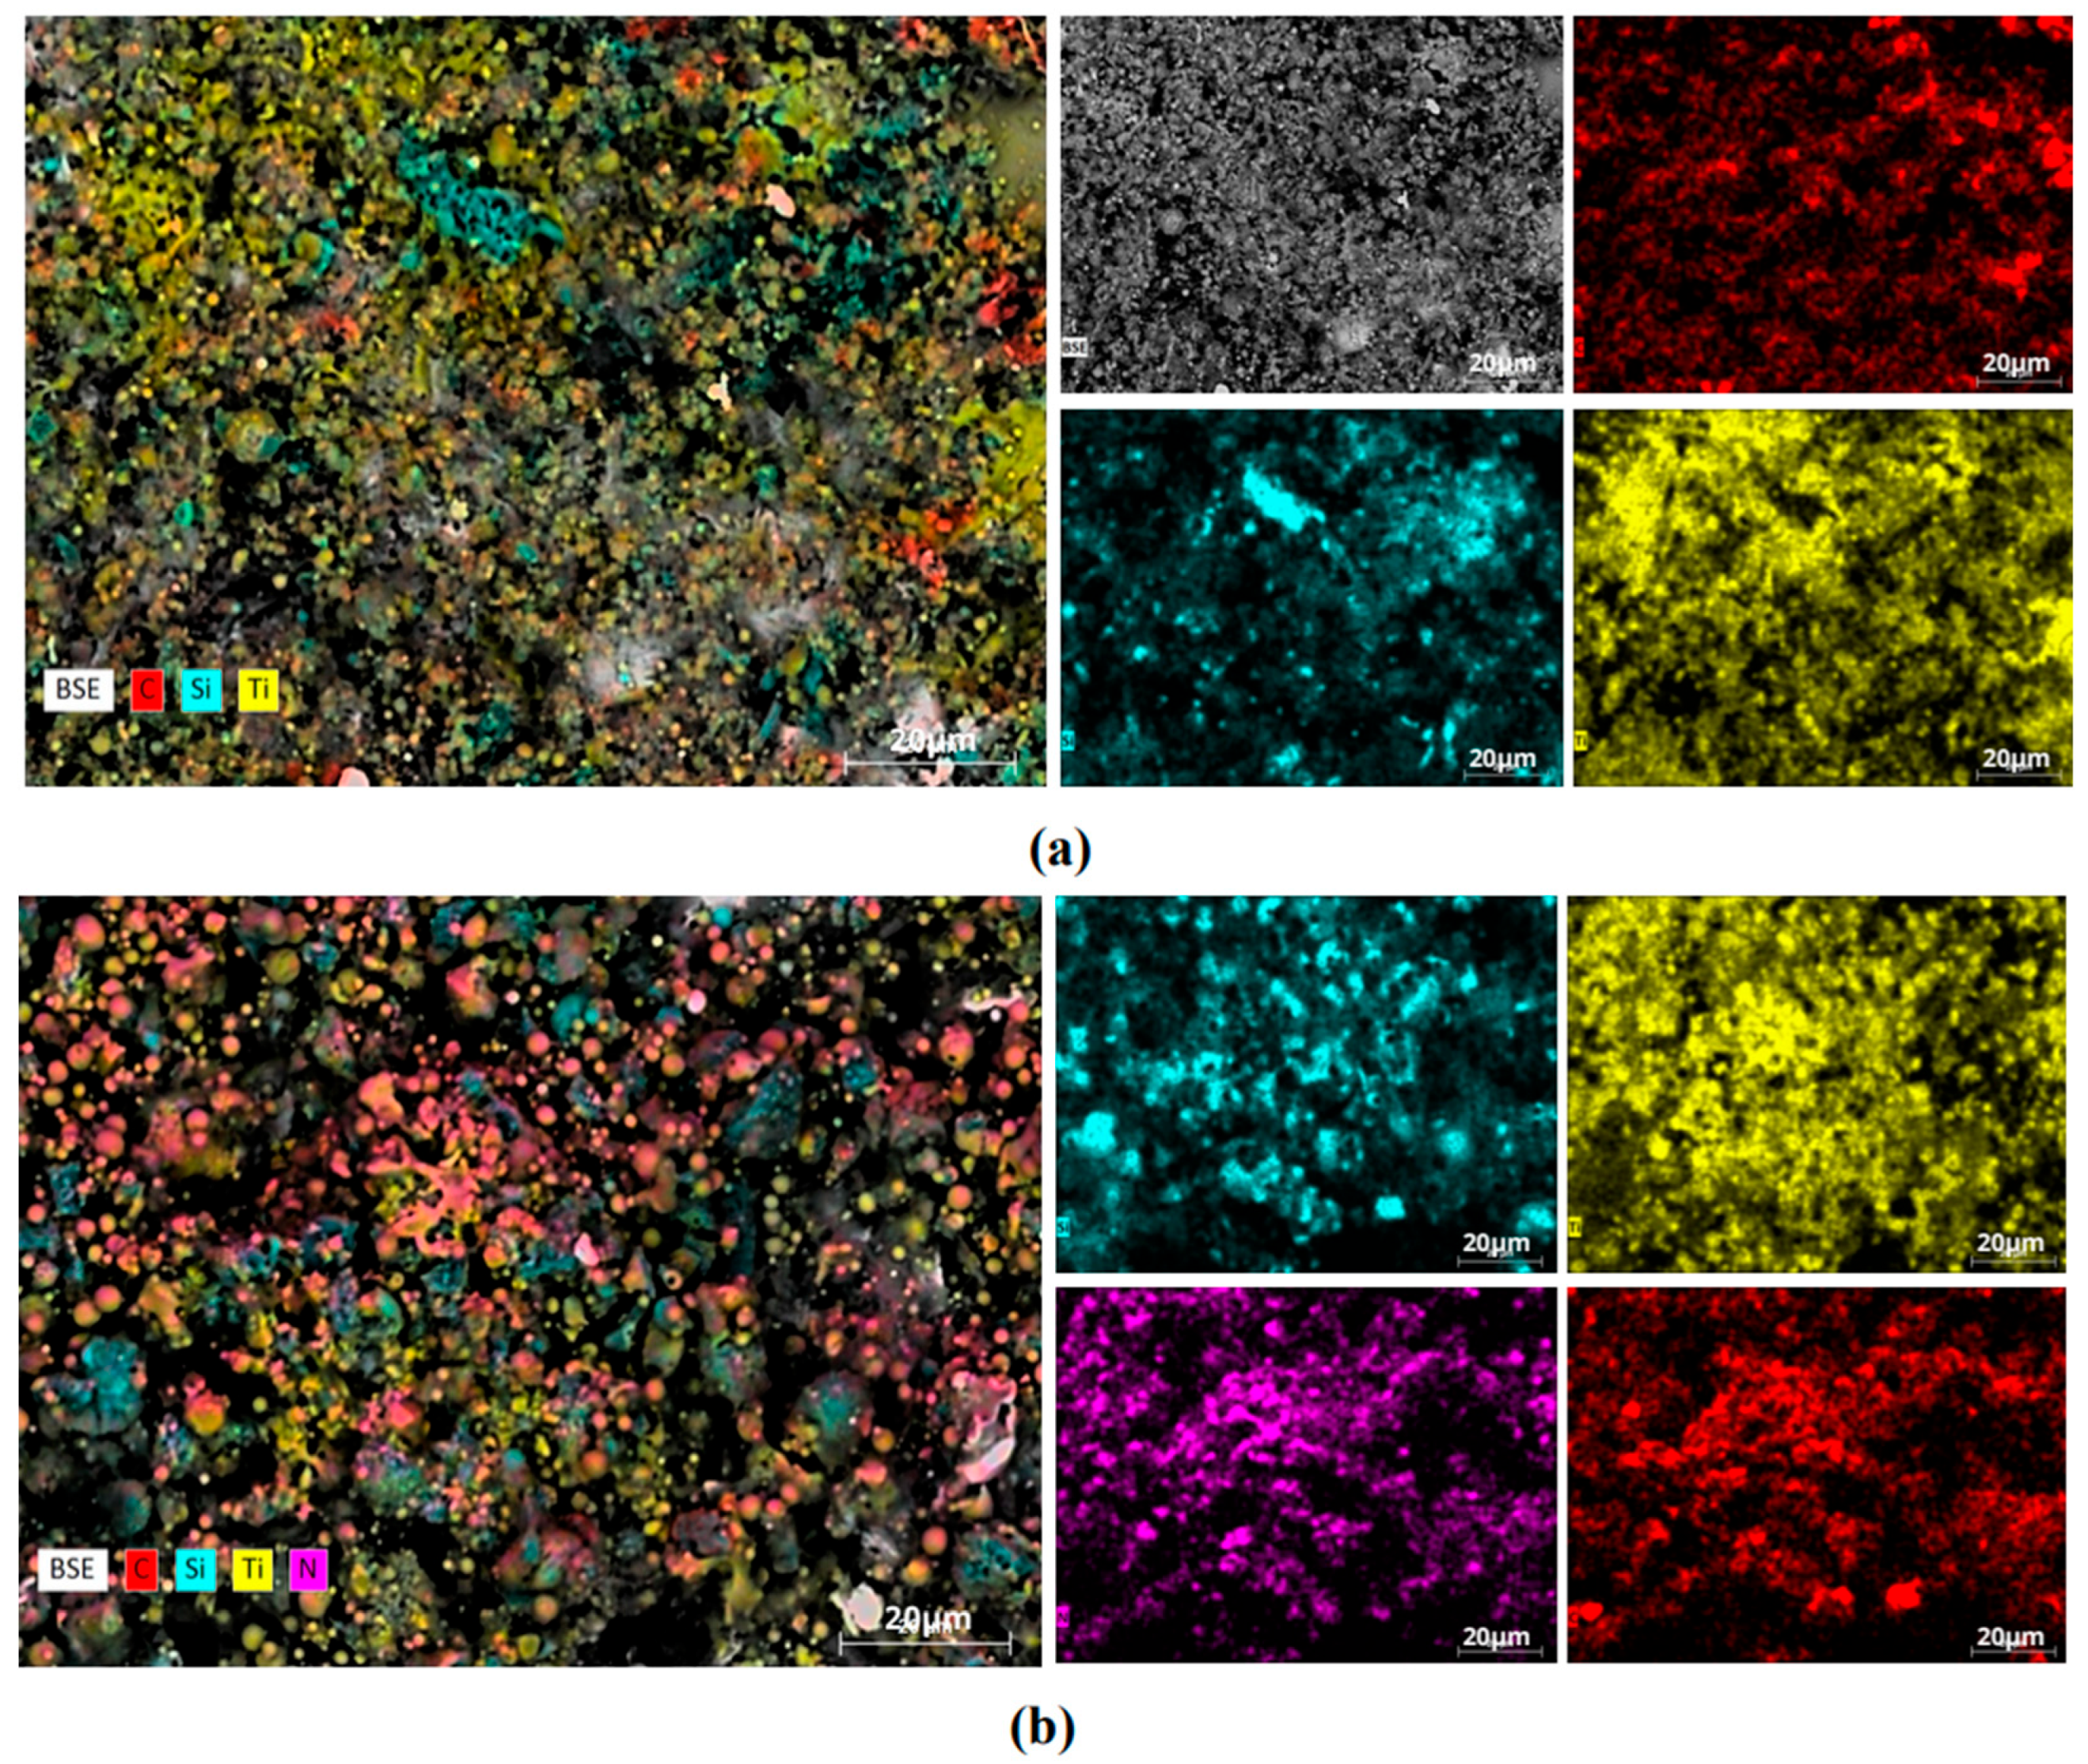
Figure 5 presents the SEM micrographs of the coatings together with the corresponding EDS elemental maps. Figure 4a shows sample TiSiC-2 (500 A), while Figure 4b demonstrates sample TiSiCN-3 (600 A) as a representative of the TiSiCN system. Both coatings exhibit relatively dense structures with well-adhered layers; however, the TiSiCN-3 coating shows a more homogeneous distribution of elements and a finer microstructure compared with TiSiC-2.
Figure 5.
SEM micrographs and EDS elemental maps of TiSiC-2 (a) and TiSiCN-3 (b).
The microstructures and elemental distributions of the TiSiC-2 and TiSiCN-3 coatings are shown in Figure 5. The TiSiC-2 coating exhibits a uniform distribution of Ti, Si, and C, indicating a dense and homogeneous structure with minimal porosity. In contrast, the TiSiCN-3 coating shows a distinct nitrogen signal, confirming the formation of a Ti(C,N) solid solution, as supported by the XRD peak shift toward higher diffraction angles.
Elemental mapping reveals a uniform distribution of Ti, Si, C, and N, forming a Ti(C,N)-based matrix with dispersed SiC and Si3N4 phases that enhance hardness and thermal stability. The TiSiCN-3 sample demonstrates the most uniform morphology and optimal phase composition, confirming that the selected spraying parameters produced dense nanostructured coatings with improved mechanical and thermal properties.
It should be noted that EDS provides limited quantitative accuracy for light elements such as C and N; therefore, the results are treated as semi-quantitative and are used only to assess relative elemental distribution.
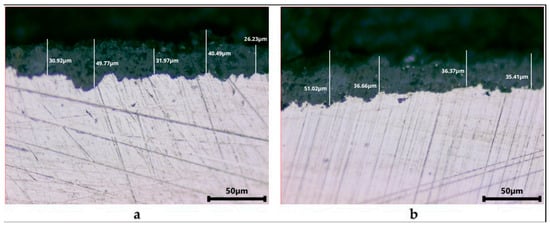
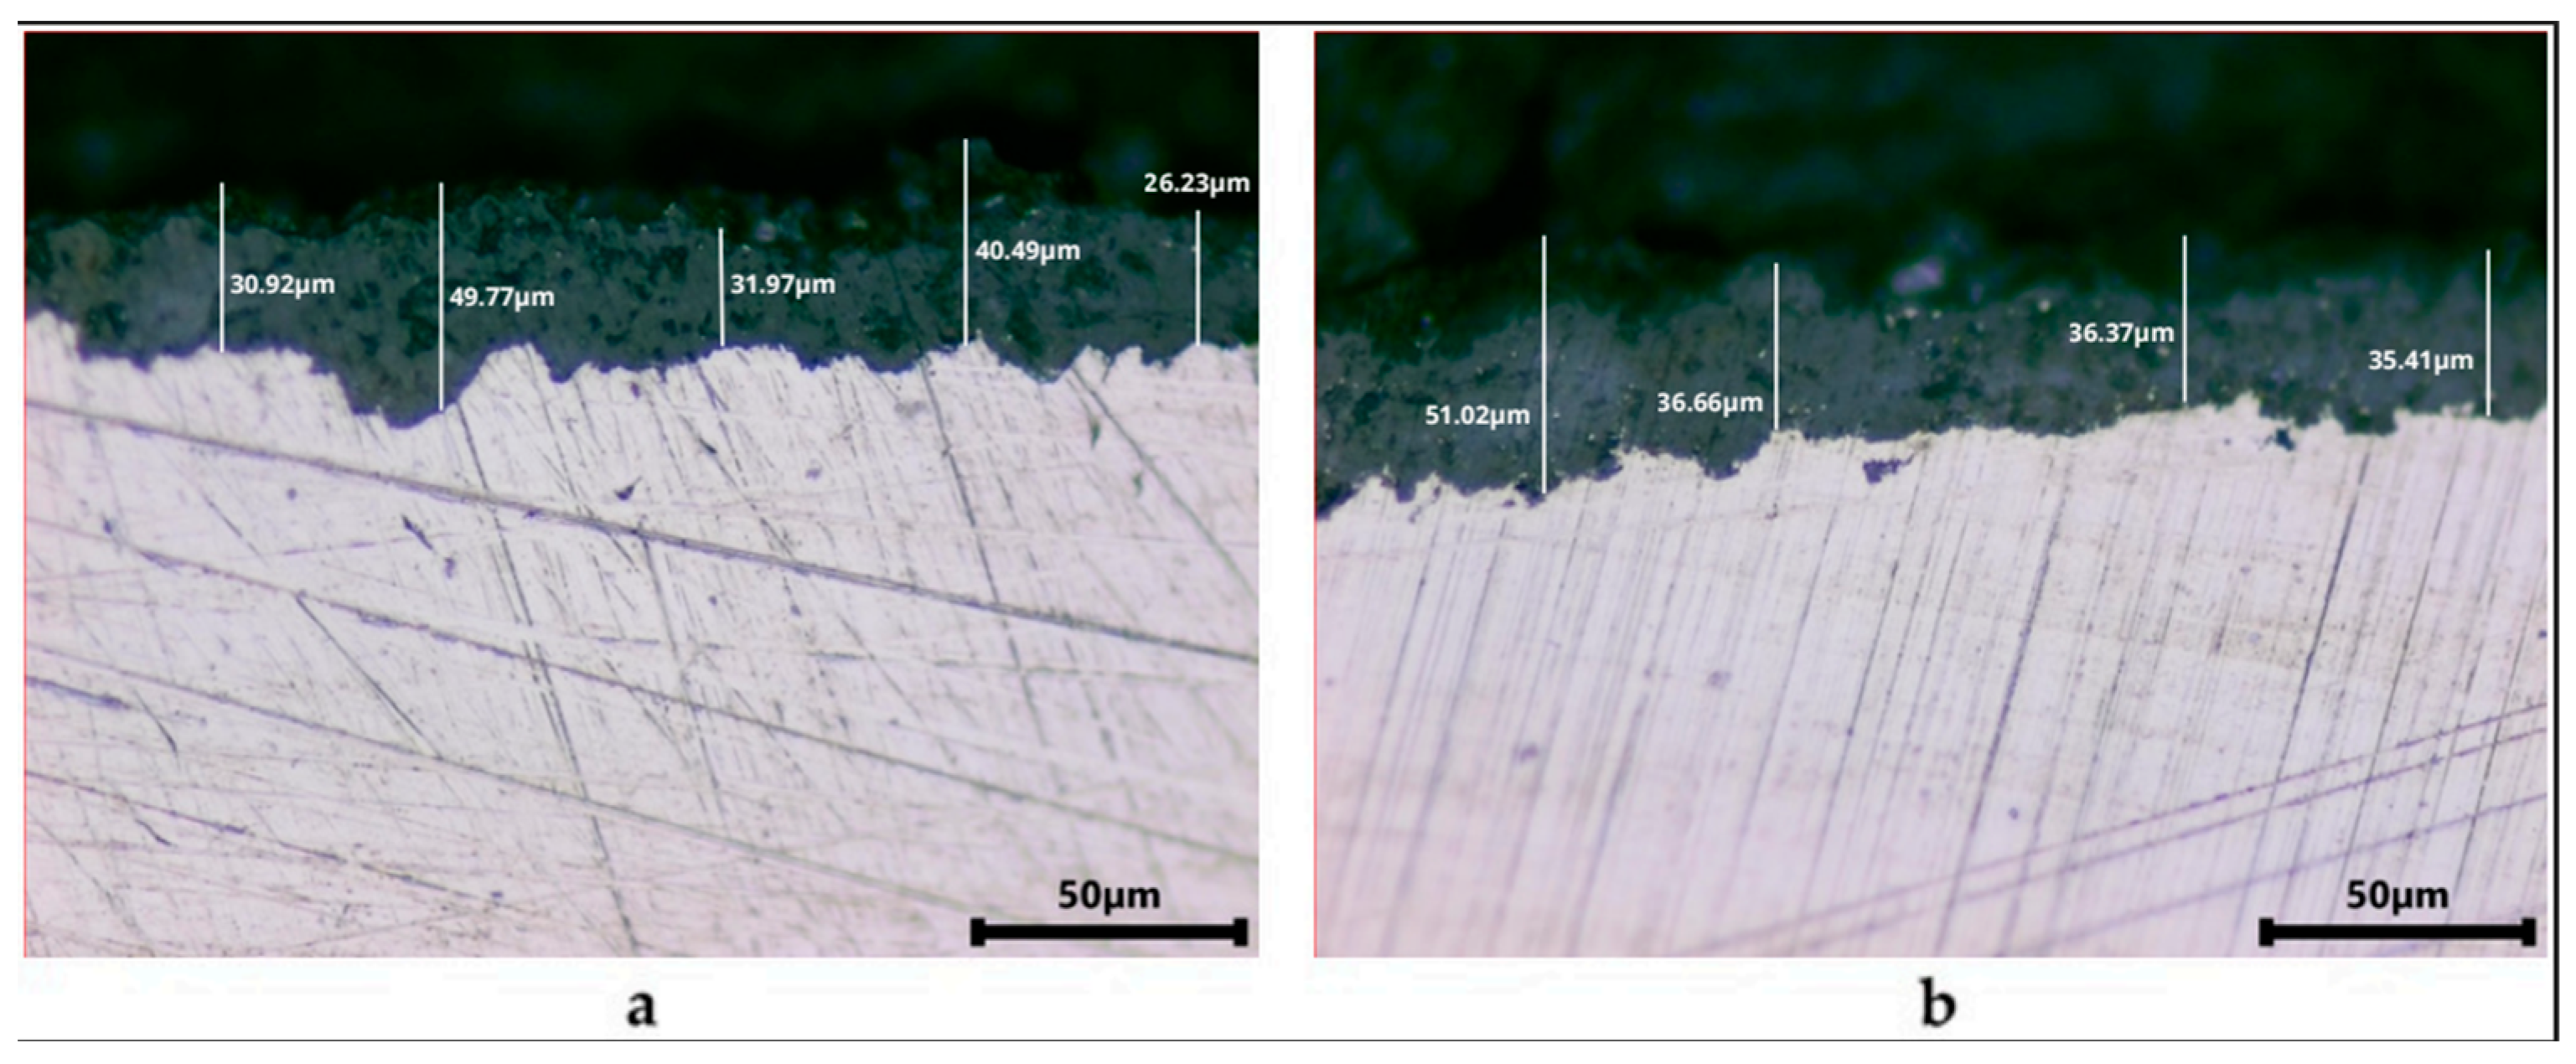
Figure 6 presents cross-sectional micrographs of coatings obtained by reactive plasma spraying. Two representative samples corresponding to the Ti + SiC and TiCN + SiC + Si systems were selected to illustrate the structural features and coating thickness distribution.
Figure 6.
Cross-sectional micrographs with coating thickness measurements for coatings: TiSiC-2 (a) and TiSiCN-3 (b).
The average coating thickness for the Ti + SiC sample is approximately 35.5 µm, while that for the TiCN + SiC + Si sample reaches about 39.9 µm. The higher and more uniform thickness of the TiCN + SiC + Si coating indicates improved adhesion to the substrate and a denser structure, which can be attributed to the presence of nitrogen and silicon in the initial powder composition.
In both cases, the coatings exhibit good adhesion to the substrate, with no visible cracks or delamination at the interface and uniform thickness distribution across the surface. The Ti + SiC coating shows minor local variations in thickness (26–50 µm), whereas the TiCN + SiC + Si coating demonstrates a more stable layer thickness (35–51 µm), indicating better process control and higher structural homogeneity.
The dense lamellar structure observed by SEM is consistent with results reported for Ti–Si–C–N coatings synthesized under similar plasma parameters [19,20,21,22].
3.3. Microhardness of TiSiC and TiSiCN Coatings
The mechanical properties of the coatings were evaluated by microhardness testing.
Table 3 presents the complete dataset of the Martens hardness (HM) measurements for both TiSiC and TiSiCN coatings, including mean values, standard deviations, minimum and maximum values, and the full measurement range (n = 10 for each coating).
Table 3.
Complete microhardness dataset for TiSiC and TiSiCN coatings.
According to the hardness data presented in Table 3, the TiSiC coating exhibits a Martens hardness of 1141.7 ± 113.9 N/mm2, whereas the TiSiCN coating shows significantly higher values, reaching 2599.2 ± 497.8 N/mm2. These HM values correspond to approximately 129 HV and 324 HV, respectively, calculated according to ISO 14577. Thus, the TiSiCN coating demonstrates more than a twofold increase in hardness compared with TiSiC. This improvement is associated with the formation of the Ti(C,N) solid solution and the presence of amorphous Si3N4/SiC boundary phases, which enhance resistance to plastic deformation and contribute to the wider hardness range observed for TiSiCN, consistent with its nanocomposite microstructure.
To ensure the reliability of the hardness measurements, an indentation load of 300 mN was selected with respect to the coating thickness. The resulting indentation depth was 2.0–2.5 µm, while the coating thickness determined from cross-sectional SEM (Figure 6) was 35–40 µm. Therefore, the penetration depth remained below 10% of the coating thickness, eliminating substrate influence and fully satisfying ISO 14577.
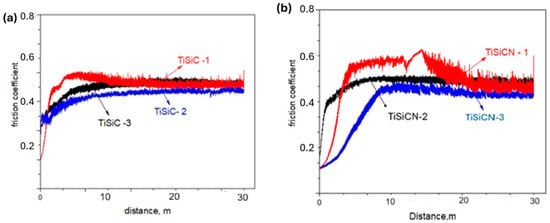
The tribological behavior of TiSiC and TiSiCN coatings was investigated under identical conditions (load 5 N, sliding speed 0.1 m/s, 90 m). The friction coefficient curves are shown in Figure 7.
Figure 7.
Coefficient of friction curves for (a) TiSiC and (b) TiSiCN coatings under identical test conditions.
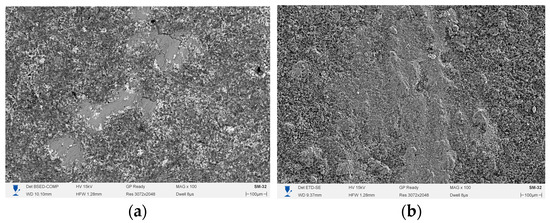
The friction coefficient of the TiSiC coatings remained at approximately 0.69, whereas the TiSiCN coatings demonstrated lower values (~0.58). Such a reduction in friction with increased Si and N content has been previously reported for Ti–Si–C–N systems synthesized by plasma-based techniques [26,27,28,29]. To clarify the tribological behavior of the investigated coatings, a microscopic examination of the wear tracks was performed. Figure 8 shows SEM images of the wear surfaces of the TiSiC-2 and TiSiCN-3 samples.
Figure 8.
SEM micromorphology of wear tracks after tribological tests: (a) TiSiC-2; (b) TiSiCN-3.
The wear track of TiSiC-2 (Figure 8a) exhibits pronounced grooves, surface fragmentation and accumulated wear debris, which are indicative of an abrasive–adhesive wear process possibly accompanied by local fatigue-related microcracking. In contrast, the TiSiCN-3 coating (Figure 8b) shows a smoother and more compact surface morphology with regions of continuous bright-phase coverage. The presence of these compact surface films may indicate the development of tribologically induced oxide–nitride layers during high-temperature sliding.
These observations are consistent with previously published results for Ti–Si–C–N nanocomposite coatings, where high-temperature friction was associated with the formation of surface oxide or oxynitride layers acting as mechanically stable lubricious films [14,20]. Although a detailed chemical analysis of the surface films was beyond the scope of the present work, the observed smoothing of the wear track and the presence of compact surface layers on TiSiCN-3 suggest that tribochemical surface modification could contribute to the lower friction coefficient measured for this coating.
Overall, the comparison of the two systems indicates that the TiSiCN coating demonstrates a more benign wear morphology under high-temperature sliding conditions, which is consistent with its improved frictional stability and may be related to the formation of protective tribochemical surface layers.
3.4. Corrosion and Oxidation Behavior
The results of the electrochemical tests are summarized in Table 4. The presented values represent averages of at least three independent measurements, with standard deviations not exceeding 10%. Compared to the uncoated stainless steel, all coated samples demonstrate a positive shift in Ecorr and a significant reduction in Icorr, leading to lower corrosion rates. For Ti + SiC coatings, the corrosion rate decreased almost fourfold, while TiCN + SiC + Si coatings exhibited an even stronger improvement, with the lowest values obtained at 500–600 A.
Table 4.
Electrochemical parameters of TiSiC and TiSiCN coatings in 3.5% NaCl solution (average values of three independent tests).
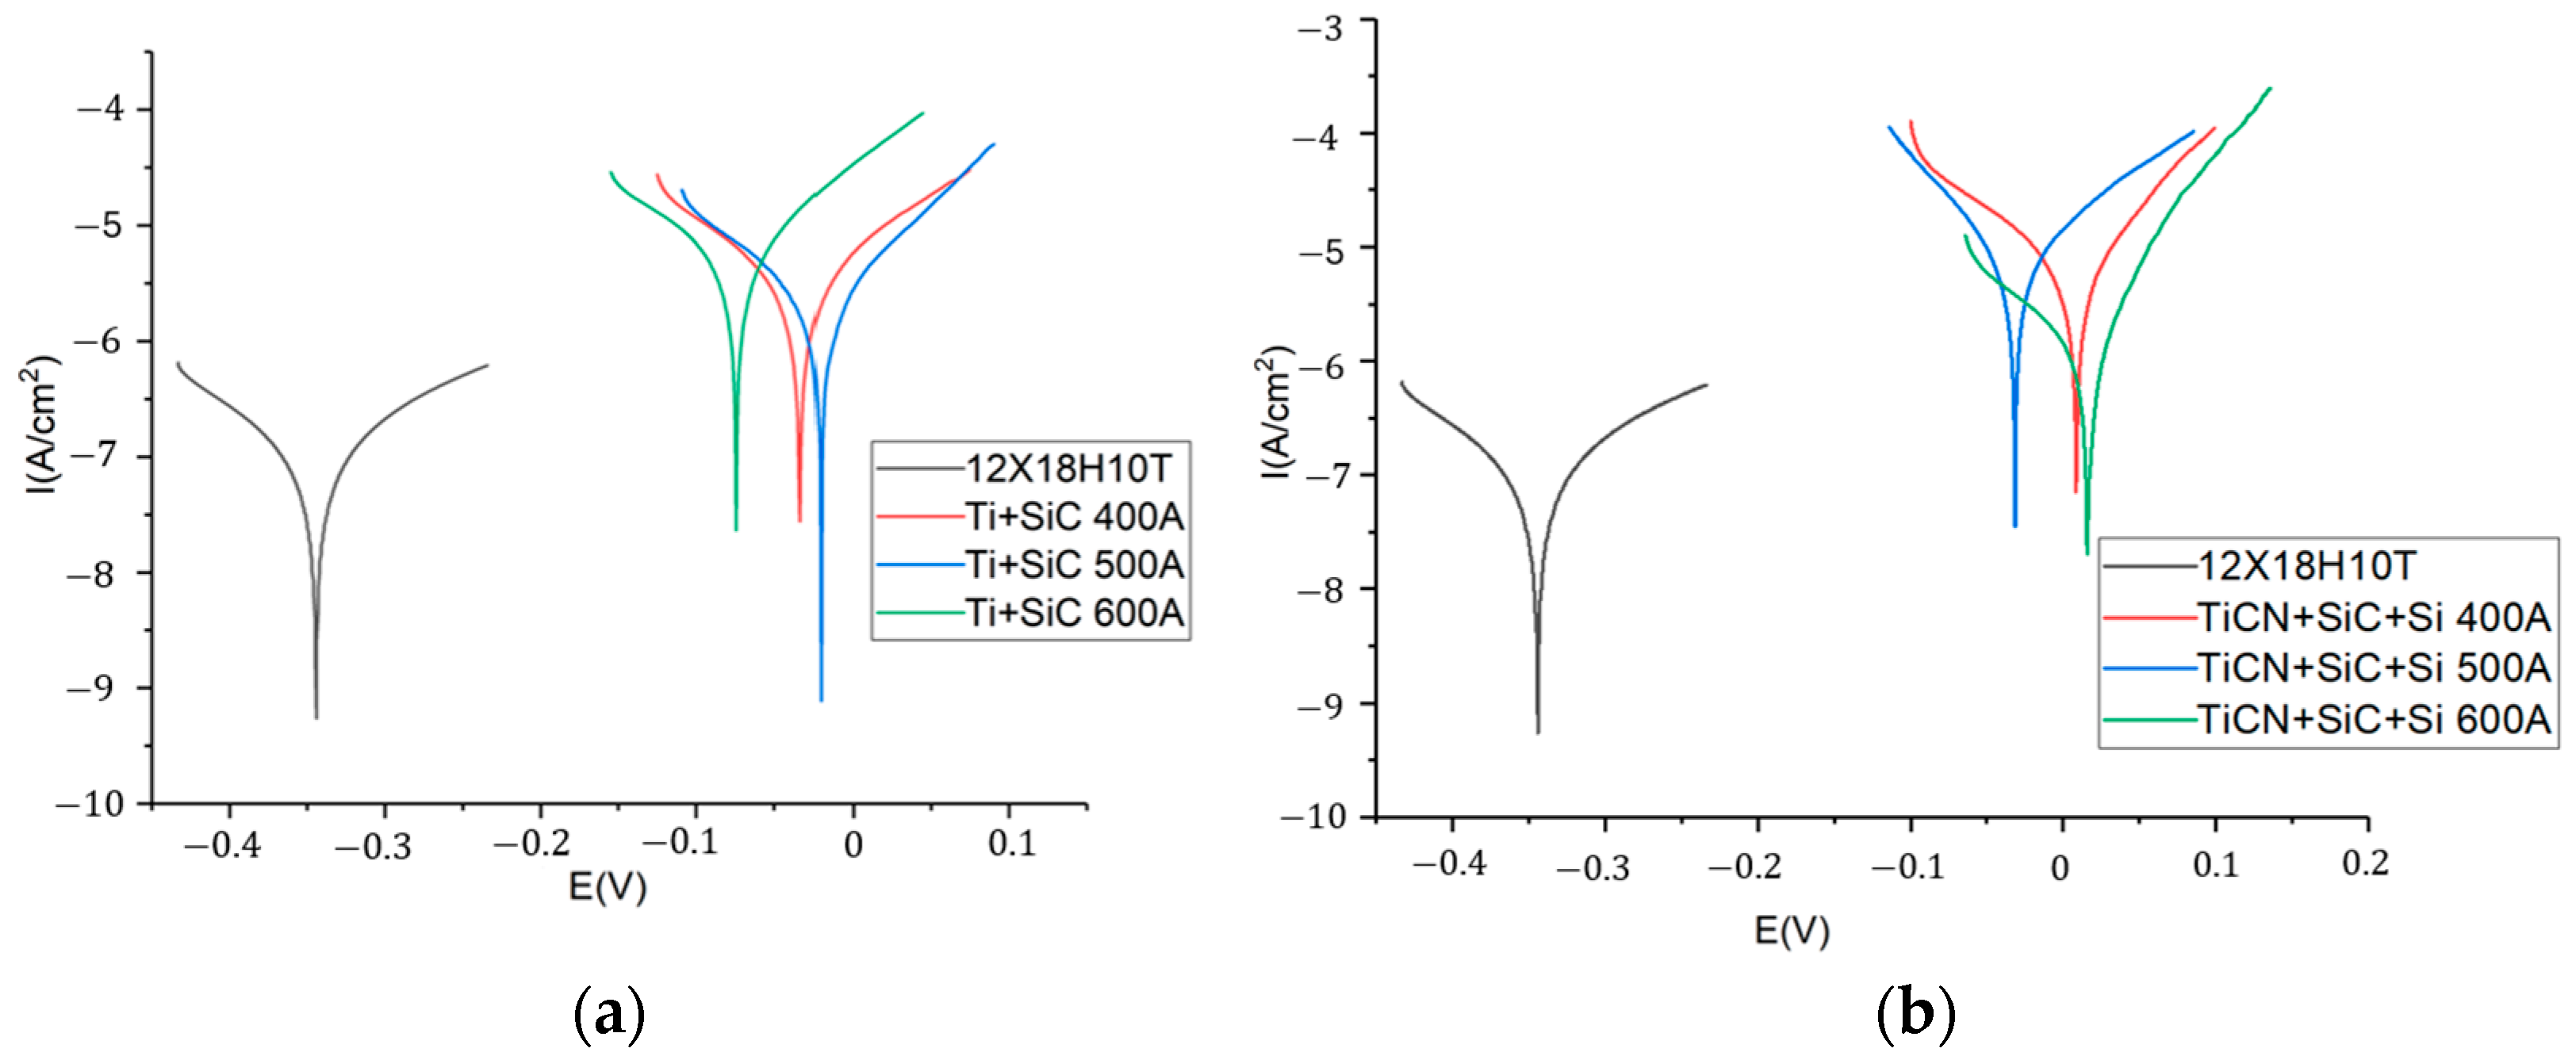
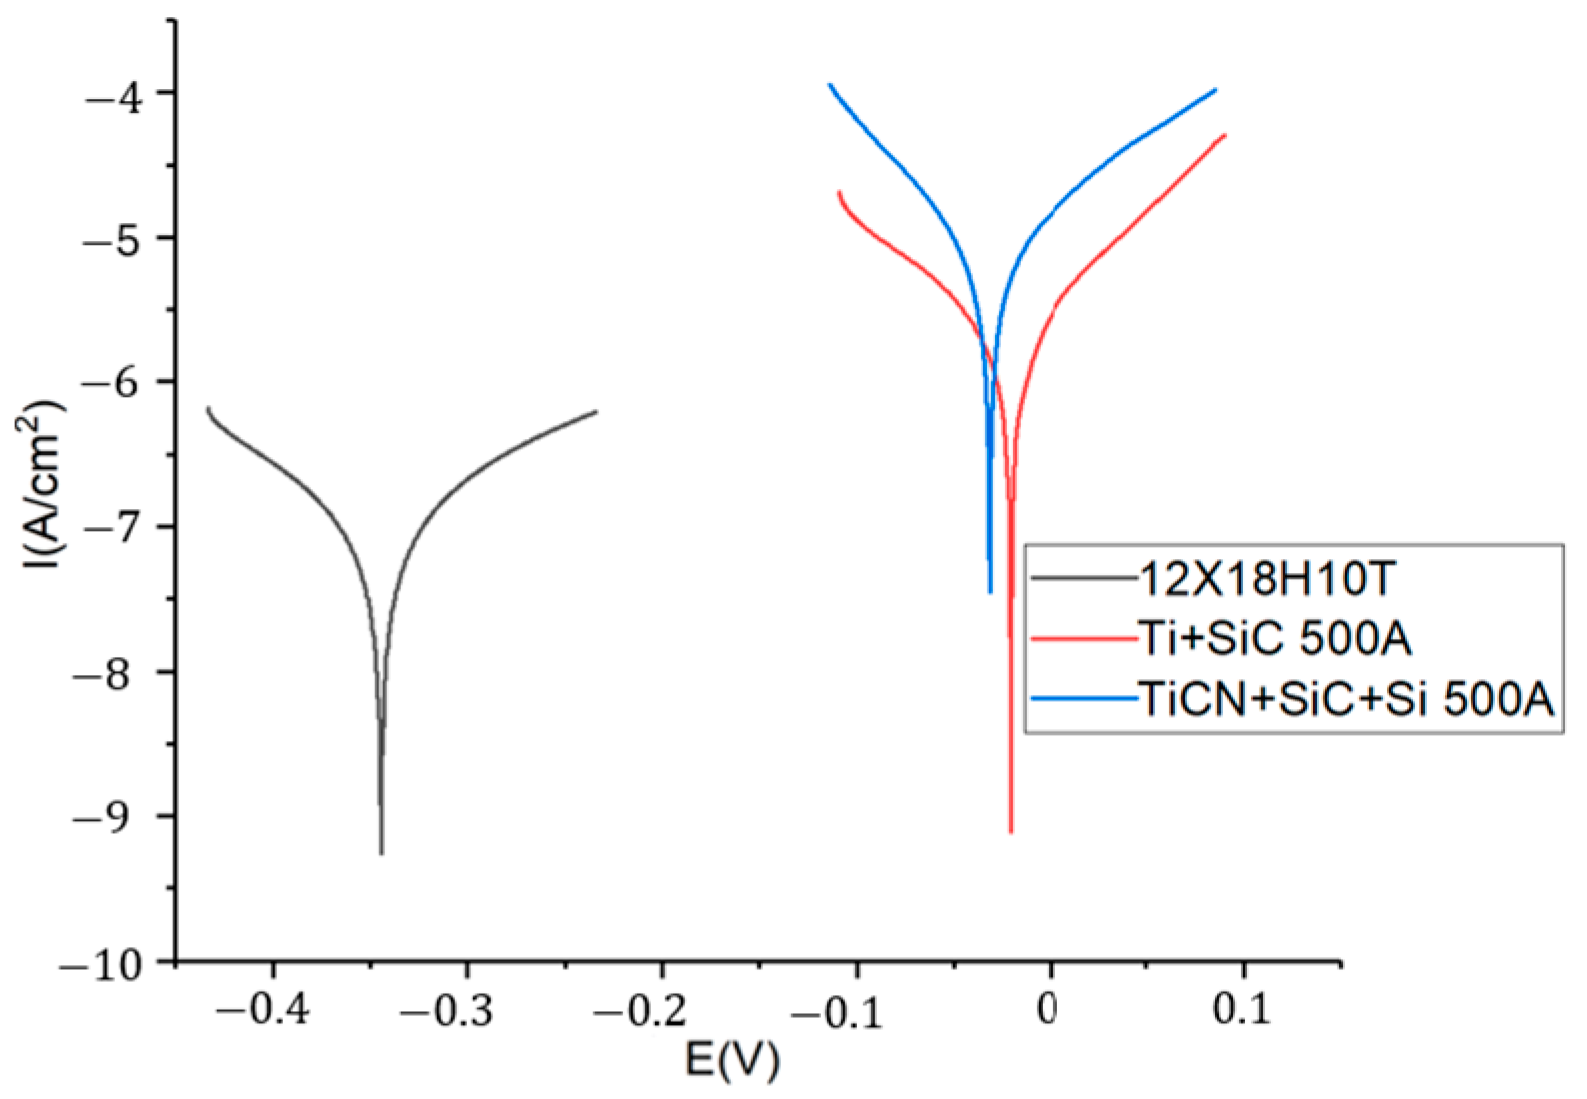
The potentiodynamic polarization curves of Ti + SiC and TiCN + SiC + Si coatings in comparison with the uncoated steel substrate are presented in Figure 9 and Figure 10.
Figure 9.
Potentiodynamic polarization curves of coatings in 3.5% NaCl: (a) Ti + SiC coatings deposited at 400, 500, and 600 A compared with uncoated 12X18H10T steel; (b) TiCN + SiC + Si coatings deposited at 400, 500, and 600 A. Representative polarization curve (n = 3); averaged parameters are listed in Table 4.
Figure 10.
Comparison of potentiodynamic polarization curves of Ti + SiC and TiCN + SiC + Si coatings deposited at 500 A in 3.5% NaCl solution. Representative polarization curve (n = 3); averaged parameters are listed in Table 4.
As shown in Figure 8, both Ti + SiC and TiCN + SiC + Si coatings exhibit a positive shift in the corrosion potential (Ecorr) and a remarkable decrease in the corrosion current density (Icorr) compared with uncoated 12X18H10T steel.
As shown in Figure 8, both Ti + SiC and TiCN + SiC + Si coatings exhibit a positive shift in the corrosion potential (Ecorr) and a remarkable decrease in the corrosion current density (Icorr) compared with uncoated 12X18H10T steel. The reported Icorr values represent apparent current density normalized to the geometric area because the real electrochemically active surface of plasma-sprayed coatings is increased due to their rough morphology. For Ti + SiC coatings (Figure 8a), the corrosion rate decreased nearly fourfold, reaching values of ~0.012 mm/year. This improvement is attributed to the formation of compact TiC and SiC phases, which reduce the number of active sites for anodic dissolution.
For TiCN + SiC + Si coatings (Figure 8b), the corrosion behavior was further enhanced: the corrosion rate decreased to ~0.008–0.009 mm/year, which is more than six times lower than that of the bare substrate. The superior performance of these coatings is explained by their denser structure and the formation of a complex passive layer composed of TiO2, SiO2, and amorphous Si3N4, effectively blocking the penetration of chloride ions. Corrosion in these coatings is thus localized only at occasional defects or pores, rather than occurring uniformly across the surface.
The comparison between the two systems clearly demonstrates that the introduction of nitrogen and additional Si phase in TiCN + SiC + Si coatings leads to stronger passivation and improved barrier properties relative to Ti + SiC coatings.
As illustrated in Figure 9, a direct comparison of the polarization curves of Ti + SiC and TiCN + SiC + Si coatings deposited at 500 A confirms the superior corrosion resistance of the latter system.
Both coatings exhibit improved behavior compared to uncoated steel; however, TiCN + SiC + Si demonstrates a more positive Ecorr and nearly 40% lower Icorr than Ti + SiC. This difference highlights the important role of nitrogen incorporation and the additional Si phase, which promote the formation of stable Ti(C,N) solid solutions and amorphous Si3N4 interlayers. These phases enhance the passivation ability of the coating and reduce the number of electrochemically active defects.
The results indicate that, under identical deposition conditions, TiCN + SiC + Si coatings provide a denser microstructure and more robust barrier properties against chloride-induced attack compared to Ti + SiC coatings. This finding is consistent with previous reports [8,14], confirming that nitrogen and silicon additions significantly enhance the corrosion resistance of Ti-based carbonitride systems.
The cyclic oxidation behavior of TiSiC and TiSiCN coatings was studied in air at 700 °C for 30 h, with intermediate weighing every 5 h. The oxidation kinetics were evaluated from the mass-gain–time (Δm–t) curves (Figure 10). The TiCN + SiC + Si coatings exhibited significantly lower mass gain (≈0.8 mg cm−2) compared to the Ti + SiC coatings (≈1.9 mg cm−2), confirming their superior oxidation resistance.
The improved behavior of TiSiCN coatings is attributed to the formation of dense, adherent oxide scales consisting mainly of TiO2 and SiO2, reinforced by amorphous Si3N4 at grain boundaries. These layers act as an effective diffusion barrier that prevents further oxygen penetration and stabilizes the coating microstructure at elevated temperatures. Similar protective mechanisms were reported by Endler et al. [8] and Wang et al. [16] for multicomponent Ti–Si–C–N systems. The synergistic effect of nitrogen and silicon thus ensures better thermal and chemical stability of the TiSiCN coatings under prolonged exposure to air.
Thus, the analysis confirms that optimizing the powder composition and spraying parameters (in particular, employing TiCN + SiC + Si coatings deposited at an optimized arc current of 500–600 A) leads to a substantial improvement in electrochemical performance. Compared to bare 12X18H10T steel (Ecorr ≈ −528 mV, Icorr = 4.44 µA/cm2, CR = 0.0506 mm/year), Ti + SiC coatings reduced the corrosion rate to ~0.012 mm/year (Ecorr ≈ −502…−515 mV, Icorr ≈ 1.07–1.11 µA/cm2). The best results were achieved for TiCN + SiC + Si coatings, which demonstrated Ecorr values of −465…−478 mV, Icorr = 0.72–0.86 µA/cm2, and corrosion rates as low as 0.008–0.009 mm/year, corresponding to more than a sixfold reduction compared with the substrate. These coatings form dense structures with effective passive films (TiO2, SiO2, Si3N4) that act as barriers against chloride-induced attack. Therefore, TiCN + SiC + Si coatings produced by reactive plasma spraying are promising for applications in marine atmospheres and other chloride-containing environments where high corrosion resistance is required.
4. Conclusions
This study presents a comprehensive investigation of TiSiC and TiSiCN coatings synthesized by reactive plasma spraying using mechanically activated powders. The research establishes clear correlations between composition, plasma parameters, microstructure, and functional performance of the coatings.
In the Ti + SiC system, the dominant phases were TiC and β-SiC, which provided sufficient hardness and erosion resistance but limited oxidation stability due to residual metallic titanium and TiO2 inclusions. In contrast, the TiCN + SiC + Si system enabled the formation of a stable TiCxN1−x solid solution with amorphous Si3N4 and SiC boundary phases, leading to microstructural densification, reduced porosity, and improved chemical and thermal stability.
Among all coatings, TiSiCN layers exhibited superior hardness (approximately 324 HV, corresponding to 2599 N/mm2), minimal erosion mass loss (<1 mg), and enhanced adhesion compared with TiSiC coatings. High-temperature tribological tests (400–600 °C) demonstrated that TiSiCN coatings maintained the lowest and most stable friction coefficients (0.45–0.55 at 600 °C) due to the in situ formation of thin TiO2–SiO2–Si3N4 tribo-oxidized layers that provided self-lubricating behavior and prevented crack propagation.
Electrochemical tests in 3.5 wt.% NaCl solution revealed a sixfold reduction in corrosion rate—from 0.0506 to 0.008 mm·year−1—compared with uncoated stainless steel. The optimized TiCN + SiC + Si composition deposited at 500–600 A produced dense nanostructured TiSiCN coatings with an excellent combination of hardness, wear, oxidation, and corrosion resistance.
The key novelty of this work lies in the first comparative study of TiSiC and TiSiCN coatings produced by reactive plasma spraying using mechanically activated powders, demonstrating the synergistic role of nitrogen and silicon in enhancing structural integrity and functional performance.
Author Contributions
Conceptualization, L.S.B. and B.K.R.; Methodology, L.S.B.; Investigation, L.S.B.; Data curation, L.S.B.; Writing—original draft preparation, L.S.B.; Writing—review and editing, B.K.R.; Supervision, B.K.R. All authors have read and agreed to the published version of the manuscript.
Funding
This research was funded by Committee of Science of the Ministry of Science and Higher Education of the Republic of Kazakhstan, grant number AP19175967.
Institutional Review Board Statement
Not applicable.
Data Availability Statement
Dataset available on request from the authors.
Conflicts of Interest
Lazat S. Baimoldanova and Bauyrzhan K. Rakhadilov were employed by the company Plasma Science LLP. They declare that the research was conducted in the absence of any commercial or financial relationships that could be construed as a potential conflict of interest.
References
- Arya, R.K.; Verros, G.D.; Davim, J.P. (Eds.) Functional Coatings: Innovations and Challenges; John Wiley & Sons: Hoboken, NJ, USA, 2024. [Google Scholar]
- Atta, S.; Dash, S.; Mathew, A.T.; NarendraKumar, U. Recent developments on titanium-based mono and multilayer nitride films deposited through HiPIMS. Next Mater. 2025, 9, 100983. [Google Scholar] [CrossRef] [Scilit]
- Barshilia, H.C.; Deepthi, B.; Rajam, K.S. Transition metal nitride-based nanolayered and nanocomposite coatings as novel superhard materials. In Nanostructured Thin Films and Coatings; CRC Press: Boca Raton, FL, USA, 2010; pp. 427–480. [Google Scholar] [CrossRef] [Scilit]
- Maksakova, O.V.; Pogrebnjak, A.D.; Buranich, V.V.; Ivashchenko, V.I.; Baimoldanova, L.S.; Rokosz, K.; Raaen, S.; Malovana, N. Theoretical and experimental investigation of multilayer (TiAlSiY)N/CrN coating before and after gold ions implantation. High Temp. Mater. Process. 2021, 25, 57–70. [Google Scholar] [CrossRef] [Scilit]
- Skakov, M.; Bayandinova, M.; Kozhakhmetov, Y.; Tuyakbaev, B. Microstructure and corrosion resistance of composites based on ultra-high molecular weight polyethylene in acidic media. Coatings 2025, 15, 89. [Google Scholar] [CrossRef] [Scilit]
- Ma, S.; Xu, K. Influence of Si content on nanostructured Ti–Si–N films coated by pulsed-dc plasma-enhanced CVD. Surf. Coat. Technol. 2004, 184, 182–187. [Google Scholar] [CrossRef] [Scilit]
- Abraham, S.; Choi, E.Y.; Kang, N.; Kim, K.H. Microstructure and mechanical properties of Ti–Si–C–N films synthesized by plasma-enhanced CVD. Surf. Coat. Technol. 2007, 202, 915–919. [Google Scholar] [CrossRef] [Scilit]
- Endler, I.; Höhn, M.; Schmidt, J.; Scholz, S.; Herrmann, M.; Knaut, M. Ternary and quaternary TiSiN and TiSiCN nanocomposite coatings obtained by chemical vapor deposition. Surf. Coat. Technol. 2013, 215, 133–140. [Google Scholar] [CrossRef] [Scilit]
- Li, J.; Wang, Y.; Yao, Y.; Yu, L.; Zhang, Y. Structure and tribological properties of TiSiCN coating on Ti6Al4V by arc ion plating. Thin Solid Film. 2017, 644, 115–119. [Google Scholar] [CrossRef] [Scilit]
- Panjan, P.; Drnovšek, A.; Gselman, P.; Čekada, M.; Panjan, M. Review of growth defects in thin films prepared by PVD techniques. Coatings 2020, 10, 447. [Google Scholar] [CrossRef] [Scilit]
- Huang, Y.; Wang, X.; Jin, B.; Wen, P.; Dong, W.; Wang, D.; Lan, W. Performance comparison and mechanistic investigation of TiN coatings fabricated by RPS and APS. Mater. Today Commun. 2025, 36, 113543. [Google Scholar] [CrossRef] [Scilit]
- Qin, Y.F.; Zhu, L.Y.; He, J.N.; Chen, C.S.; Wang, J.; Fan, J.J. Microstructure and tribological properties of TiCN–Al2O3 composite coatings fabricated by reactive plasma spraying. Vacuum 2018, 147, 149–157. [Google Scholar] [CrossRef] [Scilit]
- Zhang, F.; He, J.; Chen, K.; Qin, Y.; Li, C.; Yin, F. Microstructure evolution and mechanical properties of TiCN–Cr nano/micro composite coatings prepared by reactive plasma spraying. Appl. Surf. Sci. 2018, 427, 905–914. [Google Scholar] [CrossRef] [Scilit]
- Wu, Z.; Li, S.; Zhou, F. Electrochemical and tribological properties of TiSiCN coatings in coolant. Mater. Sci. (Medžiagotyra) 2019, 25, 548–553. [Google Scholar] [CrossRef] [Scilit]
- He, J.; Liu, J.; Zhao, H.; Qin, Y.; Fan, J. High-temperature heat treatment of plasma-sprayed Ti–Si–C–Mo coatings: Effects on microstructure and tribological performance. Coatings 2024, 14, 109. [Google Scholar] [CrossRef] [Scilit]
- Wang, Y.; Yan, M.; Yang, Y. High-temperature solid particle erosion behavior of plasma-sprayed ceramic coatings. J. Therm. Spray Technol. 2021, 30, 1227–1240. [Google Scholar] [CrossRef] [Scilit]
- Baimoldanova, L.; Rakhadilov, B.; Kengesbekov, A.; Kuanyshbai, R. Influence of mechanical activation on the evolution of TiSiCN powders for reactive plasma spraying. Crystals 2024, 14, 1005. [Google Scholar] [CrossRef] [Scilit]
- Pogrebnjak, A.; Buranich, V.; Ivashchenko, V.; Baimoldanova, L.; Rokosz, K.; Raaen, S.; Raaen, S.; Zukowski, P.; Opielak, M.; Rakhadilov, B.; et al. The effect of substrate treatment on the properties of TiAlSiYN/CrN nanocomposite coatings. Surf. Interfaces 2022, 30, 101902. [Google Scholar] [CrossRef] [Scilit]
- Meng, W.J.; Zhang, X.D.; Shi, B.; Tittsworth, R.C.; Rehn, L.E. Microstructure and properties of Ti–Si–C–N coatings. Ceram. Int. 2018, 44, 11839–11845. [Google Scholar] [CrossRef] [Scilit]
- Zhou, J.; Fan, X.; Chen, H.; Feng, D. Effect of arc current on TiN coatings prepared by arc ion plating. Vacuum 2020, 182, 109369. [Google Scholar] [CrossRef] [Scilit]
- Gkomoza, P.; Lampropoulos, G.S.; Vardavoulias, M.; Pantelis, D.I.; Karakizis, P.N.; Sarafoglou, C. Microstructural investigation of porous titanium coatings, produced by thermal spraying techniques, using plasma atomization and hydride-dehydride powders, for orthopedic implants. Surf. Coat. Technol. 2019, 357, 947–956. [Google Scholar] [CrossRef] [Scilit]
- Angra, S.; Thakur, L.; Singh, J. Effect of argon flow rate on the weld bead characteristics of TIG coating. In IOP Conference Series: Materials Science and Engineering; IOP Publishing: Bristol, UK, 2020; Volume 804, p. 012016. [Google Scholar] [CrossRef] [Scilit]
- Fouad, O.A.; Lin, H.-Y.; Shah, S.I. Reactively Magnetron Sputter-Deposited Ti (C,N) Nanocomposite Thin Films: Composition and Thermal Stability. J. Coat. Sci. Technol. 2018, 5, 42–49. [Google Scholar] [CrossRef] [Scilit]
- Rakhadilov, B.; Kengesbekov, A.; Kylyshkanov, M.; Bayatanova, L.; Amangeldyevna, A.S.; Bayandinova, M. Environmental benefits of fluorogypsum reuse in the production of construction materials. Buildings 2024, 14, 3618. [Google Scholar] [CrossRef] [Scilit]
- Ceschini, L.; Palombarini, G.; Sambogna, G. Frictional behaviour and wear resistance of TiN-based PVD coatings dry sliding against TiN-coated tool steel. Metall. Ital. 1999, 91, 45–51. [Google Scholar]
- Pogrebnjak, A.; Ivashchenko, V.; Bondar, O.; Beresnev, V.; Sobol, O.; Załęski, K.; Jurga, S.; Coy, E.; Konarski, P.; Postolnyi, B. Multilayered vacuum-arc nanocomposite TiN/ZrN coatings before and after annealing: Structure, properties, first-principles calculations. Mater. Charact. 2017, 134, 55–63. [Google Scholar] [CrossRef] [Scilit]
- Wei, R.; Rincon, C.; Langa, E.; Yang, Q. Microstructure and tribological performance of nanocomposite Ti–Si–C–N coatings deposited using hexamethyldisilazane precursor. J. Vac. Sci. Technol. A 2010, 28, 1126–1132. [Google Scholar] [CrossRef] [Scilit]
- Qin, Y.; Jiao, Q.; Zheng, G.; Zhang, F.; He, J.; Yin, F. Effects of spray distance on the microstructure and mechanical properties of reactive plasma sprayed TiCN coatings. Ceram. Int. 2018, 44, 17230–17239. [Google Scholar] [CrossRef] [Scilit]
- Smirnova, K.V.; Bondar, O.V.; Borba-Pogrebnyak, S.O.; Kravchenko, Y.O.; Beresnev, V.M.; Zhollybekov, B.; Baimoldanova, L. Microstructure and mechanical properties of (TiAlSiY)N nanostructured coatings. In Proceedings of the IEEE 7th International Conference on Nanomaterials: Applications & Properties (NAP 2017), Odessa, Ukraine, 10–15 September 2017; Volume 2, pp. 01FNC13-1–01FNC13-4. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2025 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license (https://creativecommons.org/licenses/by/4.0/).