


Abstract
Rubber is a crucial sealing material in the petroleum industry. Due to increasingly stringent industrial development, safety performance requirements are becoming extremely high, resulting in higher oil resistance requirements for rubber. HNBR exhibits good heat resistance, high tensile strength, tear strength, and excellent wear resistance. However, a certain degree of aging will also occur in the actual service process, which will affect the service life of rubber. In order to explore the factors affecting the aging behavior of HNBR vulcanizates in an oil–water environment at 150 °C, HNBR vulcanizates were aged in an independent environment. IR (Infrared) spectroscopy analysis (FTIR), crosslinking density analysis, dynamic mechanical analysis (DMA), and scanning electron microscopy (SEM) testing were used to characterize the microstructural and morphological changes in HNBR vulcanizates before and after aging. The aging mechanism of HNBR vulcanizates in different environments was obtained. Since factors such as rubber fillers remained constant throughout the experimental process, the influence of formulation variables on aging was disregarded.
1. Introduction
Entering the 21st century, non-renewable energy sources have become increasingly scarce, with oil being crucial to the lifeblood of nations. As a result, the extraction and protection of oil have become more and more important. Rubber, as a functional polymer material, plays a crucial role in the process of oil extraction and transportation [1]. It is used in applications such as oil and gas transfer hoses, sealing rings, and rubber packers, contributing significantly to the development and operation of oil and gas fields. The functions it performs are irreplaceable by other materials [2,3,4]. With the shortage of oil resources and the development of the petrochemical industry, the exploration and development of oil resources have become increasingly difficult [5]. During the exploration and development process, challenges are posed by the extreme conditions of high temperatures and high pressures. Under such complex environments, the efficiency of oil and gas development is inevitably limited. Additionally, oil and gas leaks are highly likely during extraction and transportation, posing significant environmental hazards. Since rubber is also a polymer material primarily composed of hydrocarbon bonds, it has a certain level of compatibility with oil. Therefore, when exposed to high temperature, high pressure, and complex oil–water environments for extended periods, rubber inevitably undergoes aging, leading to severe deterioration of its mechanical and sealing properties [6,7,8,9]. This significantly shortens its service life. As a result, the aging performance and service life of rubber play a crucial role in the development and transportation of oil and gas. Furthermore, prolonged exposure to air can also cause aging in rubber, further degrading its mechanical and sealing properties, thus reducing its overall lifespan [7,10]. In light of this situation, it is necessary to conduct research on the aging of rubber sealing materials in complex environments, investigating the aging mechanisms and failure mechanisms. This research aims to identify methods to reduce the aging phenomena of rubber during its service life.
The molecular chain of nitrile rubber (NBR) contains unsaturated butadiene units, forming a relatively unsaturated carbon chain rubber. As a result, nitrile rubber is highly susceptible to aging under high-temperature conditions, leading to permanent failure of the rubber [11]. Therefore, under conditions of 120 °C, nitrile rubber is not an ideal sealing material. By selectively and controllably hydrogenating the double bonds of acrylonitrile-butadiene copolymer (NBR), hydrogenated nitrile rubber (HNBR) is produced. HNBR is the product obtained by hydrogenating nitrile rubber through a hydrogenation reaction [12]. The hydrogenation process significantly reduces the molecular unsaturation, improving its properties compared to NBR. HNBR exhibits enhanced heat resistance, improved mechanical properties, and better wear resistance than NBR. However, under extremely harsh conditions, both HNBR and NBR undergo significant aging and degradation. During the aging process, phenomena such as chain scission, oxidative crosslinking, and molecular chain rearrangement usually occur, leading to a reduction in the rubber’s performance [13,14]. Both nitrile rubber and hydrogenated nitrile rubber contain active cyano (-CN) groups. The difference between the two is the varying content of double bonds (-C=C-) [15]. These active groups are responsible for the aging and degradation of the rubber during its use. Additionally, the crosslinking structure and the content of cyano groups in the molecular chain are important factors influencing rubber aging.
Research on the aging and degradation of HNBR has shown that the concentration of residual double bonds (RDBs) may be one of the most important factors in controlling thermal air aging [16]. Oxidation reactions tend to occur preferentially at the allylic positions of unsaturated bonds. Additionally, the tertiary carbon of the ethyl side group is also susceptible to oxidation [17]. The concentration of acrylonitrile and the molecular weight (Mooney viscosity) have little impact on the thermal aging performance of HNBR. Bhattacharjee et al. studied the degradation of HNBR in the temperature range of 75 °C to 150 °C under air and nitrogen, and from room temperature to 800 °C [16]. They found that the molecular weight initially increased and then decreased after the optimal aging time. As observed by FTIR, carbonyl (C=O) and ester (-COOR) functional groups were generated through oxidation. Using ESCA, a shift in the binding energy of N1s electrons to higher values was observed, which was interpreted as oxidation occurring in the acrylonitrile units. It was hypothesized that azo methylene crosslinking occurs through the attraction of the nitrogen atom to the α-hydrogen [18]. Acrylonitrile loss occurred only during the thermal aging of HNBR, not NBR. For HNBR with 39% acrylonitrile (ACN) content, similar oxidative group evolutions were observed in the temperature range of 150 to 185 °C via FTIR [19]. At higher temperatures, imidazole crosslinking (2240 cm−1) could continue to react with adjacent cyano groups, leading to cyclization [20]. The -CN vibration band shifted to lower frequencies, and the gel content increased, indicating a higher degree of crosslinking. Verdier et al. showed that at higher temperatures (200–240 °C), HNBR could be crosslinked without the use of curing agents, as the acrylonitrile units reacted under oxidation to form crosslinked ladder-like structures similar to polyacrylonitrile [21,22]. It is believed that the crosslinking of HNBR using this method is limited to high acrylonitrile content and low residual double-bond concentrations.
Anton et al. investigated the aging of HNBR in a simulated oil and gas environment at two temperatures, 130 °C and 150 °C. The results demonstrated that temperature played a more critical role than time in the aging process: relatively moderate changes in material properties were observed at 130 °C, whereas severe deterioration occurred at 150 °C. In particular, after nine months of aging at 150 °C, the cyano groups (C≡N) in HNBR were completely converted into amide groups. This chemical transformation led to a sharp increase in the glass transition temperature from approximately −16 °C to about +70 °C, accompanied by a significant rise in hardness and worsening of compression set. Consequently, the material underwent a transition from an elastomer to a polyamide-like state [23]. Angela Longo et al. investigated the issue of unclear images of materials with 2D nanostructures, such as graphene, under SEM, proposing and validating a method to significantly enhance image contrast by tilting the sample at a large angle (close to 90°). Using a specially designed aluminum slotted specimen stub to achieve vertical fixation and manual tilting of the sample, the results demonstrate that the strongly tilted view substantially increases both the gray levels and contrast of the images: the number of gray levels rises by 31.4%–40.2%, and the area under the curve increases by 30.1%–61.1%. Consequently, key morphological features such as the edges, defects, and folds of the nanosheets are clearly revealed [24].
Compared to previous studies, the present work departs from the research paradigm based on a single standard environment. Instead, it innovatively separates and systematically recombines key environmental factors such as oil, water, and oxygen, allowing for a comprehensive investigation into the evolution of mechanical properties of samples before and after aging under different environmental conditions. In terms of characterization methodology, this study integrates multiple analytical techniques, including crosslinking density measurements, SEM surface morphology observation, infrared spectroscopy analysis, and dynamic mechanical analysis. This integrated approach enables a multiscale correlation and systematic interpretation of the chemical structure, micro-morphology, and macroscopic performance of the aged products. Building on these analyses, the aging mechanism of HNBR in high-temperature oil–water environments has been conclusively elucidated.
2. Experimental Section
2.1. Materials and Reagents
Hydrogenated Nitrile Butadiene Rubber (HNBR): Produced by Zeon Corporation, Tokyo, Japan, with acrylonitrile contents of 50%; Dicumyl Peroxide (DCP): Used as a curing agent to generate crosslinks, provided by Shijiazhuang Fat Chemical Technology Co., Ltd. (Shijiazhuang, China); Trimethylolpropane Triacrylate (TAIC): Used as a co-agent for crosslinking, purchased from Aladdin Reagents (Shanghai) Co., Ltd., (Shanghai, China); Carbon Black (Model N330): Purchased from Cabot Chemicals (Tianjin) Co., Ltd., (Tianjin, China). Other reagents were of industrial grade and used directly.
2.2. Sample Preparation
A total of 100 g of HNBR uncured rubber was placed between the rolls of a two-roll mill and passed through several times. To this, 3 g of curing agent (DCP), 1 g of co-agent (TAIC), and 50 g of carbon black (N330) were added. The mixture was then wrapped into a triangular package and passed through the mill a few more times to create a homogeneous compound. A 5 g sample of the compounded rubber was taken, and its curing characteristics were measured using a rotorless vulcanization rheometer at 170 °C, from which the curing time (tc90) was determined. Approximately 50 g of the compounded rubber was placed in a 2 mm thick square mold and vulcanized in a hydraulic press at 170 °C for the duration of the tc90 time. This resulted in a 2 mm thick square sheet of vulcanized HNBR. The vulcanized rubber was then placed in a punch machine, and dumbbell-shaped specimens were formed using a dumbbell mold. These specimens served as the standard test samples for the aging experiments. Before aging, the specimens were labeled, and their mass, volume, density, and mechanical properties, including tensile strength, hardness, and elongation at break, were measured. These properties were recorded as baseline values for comparison after aging.
2.3. Aging Experiment
Firstly, 1.6 L of oil, water, or an oil–water mixture (10# diesel:water = 1:1) was added to a sealed magnetic drive high-pressure reactor with a volume of 2 L. The labeled dumbbell-shaped specimens were then immersed in the aging medium. After the reactor was tightly sealed, 1 MPa of nitrogen gas was introduced to test the sealing integrity of the reactor. The reactor was then vented to remove the oxygen, and nitrogen was continuously flushed through the system until all the oxygen was expelled. Once the oxygen was completely removed, the valve was closed tightly. The temperature inside the autoclave was raised to 150 °C, the high-pressure vessel was equipped with continuous magnetic stirring to mix the aging medium, and the test was maintained for different days after the temperature stabilized.
After different days, turn off the heating device and allow the reactor to cool naturally to room temperature. Once the internal temperature of the reactor has dropped to ambient conditions, open the reactor and remove the aged samples. Immediately measure the mass, volume, density, and mechanical properties (including hardness, tensile strength, and elongation at break) of the samples. For all aged samples, three parallel specimens were prepared, and the statistical parameters included the mean value and standard deviation.
2.4. Mechanical Properties
According to GB/T 531.1-2008 [25], the hardness was measured using an LX-A rubber Shore hardness tester. For tensile strength and elongation at break tests at room temperature, GB/T 528-2009 [26] was followed, utilizing a WDL-10 microcomputer-controlled electronic universal testing machine. The tensile rate was maintained at 500 mm/min.
To express the changes in the mechanical properties of the samples before and after aging, the mechanical property variation rate (Δf) was introduced. The formula for Δf is as follows:
where
f0 represents the mechanical property of the sample before aging;
f represents the mechanical property of the sample after aging.
2.5. Volume Variation Rate Test
After the aged samples were removed, the surface was quickly cleaned, and the volume (V) and mass (m) of the samples were measured using a JA3003J solid density balance. The volume variation rate was calculated using the following formula:
where:
V0 represents the original volume of the sample before aging;
V represents the volume of the sample after aging;
M0 represents the original mass of the sample before aging;
M represents the mass of the sample after aging.
2.6. Crosslink Density Analysis
This experiment uses the equilibrium swelling method to determine the crosslink density. Approximately 0.1 g of the sample to be tested was cut with a blade and weighed as m0, and its density ρ was measured. The sample was then dissolved in dichloromethane until swelling equilibrium was reached. Afterward, the sample was quickly removed and weighed as m1, and the weighed sample was placed in a vacuum oven at 50 °C until its mass no longer changed. The sample was then removed and weighed again as m2. The rubber volume fraction Vr of the swollen rubber is calculated using the following formula [27]:
where m0 is the original mass of the sample, m1 is the mass of the sample after swelling, m2 is the mass of the sample after swelling and subsequent drying, is the mass fraction of pure rubber in the vulcanizate, α is the percentage of mass loss during the rubber swelling process (in %), and ρs is the density of dichloromethane (1.325 g/cm3).
Due to the addition of carbon black, the Klaus correction was applied to Vr [28].
where Vr is the volume fraction of rubber in the swollen rubber phase, Vr0 is the same quantity referred to on otherwise analogous, unfilled vulcanizate, and 1 is the volume fraction of filler, taken as 0.2. c is a parameter depending on the filler, but independent of 1 and Vr0, taken as 1.17.
The rubber’s crosslink density, Ve (in mol/cm3), can be determined based on the rubber volume fraction, Vr, obtained from the swelling test using the following formula [29]:
where Vs is the molar volume of dichloromethane (Vs = 67.8 cm3/mol), and χ is the interaction parameter between HNBR and dichloromethane, which can be calculated using the following formula [27]:
where is the solubility parameter of the vulcanizate, taken as 11. And is the solubility parameter of the solvent, taken as 9.7.
2.7. IR (Infrared) Spectroscopy Analysis
Infrared spectroscopy analysis was performed using a Tensor II infrared spectrometer (Bruker, Billerica, MA, USA). The wavenumber range was set from 4000 to 600 cm−1, with 32 scans and a resolution of 4 cm−1. The samples to be tested were cut into thin slices, with an area of 1 cm2 and measured using the Attenuated Total Reflection (ATR) mode to obtain the infrared absorption spectra.
2.8. Scanning Electron Microscopy (SEM) Testing
The surface morphology of the samples was observed by fixing the samples onto a sample holder and performing a gold sputtering treatment. After gold coating, the apparent morphology of the vulcanized rubber before and after aging was examined using a Quanta 200F scanning electron microscope (SEM).
2.9. Tests of Dynamic Mechanical Analysis (DMA)
The samples were prepared into standard tensile mode specimens, and dynamic mechanical analysis (DMA) was performed using a DMA-242 dynamic mechanical analyzer. The testing temperature range was from −80 °C to 50 °C, with a heating rate of 3 °C/min, a frequency of 10 Hz, and a strain of 1%.
3. Experimental Results
3.1. Aging Study of HNBR Vulcanized Rubber in Different Environments
3.1.1. Aging Analysis of HNBR Vulcanized Rubber in a 150 °C Hot Oil Environment
Table 1 presents the changes in the mechanical properties of HNBR vulcanized rubber before and after aging in a 150 °C hot oil environment. From Table 1, it is clear that the rubber exhibits significant changes in mechanical properties and mass/volume variation when aged in a pure oil environment. Compared to the oil–water mixed environment, aging in a pure oil phase results in a more severe loss of mechanical properties. The primary reason for this is that HNBR is fully exposed to the oil environment, which greatly increases its oil absorption capacity. Under hot oil conditions, the molecular chains of rubber do not undergo structural changes; only physical expansion occurs due to oil absorption. As more oil penetrates the rubber, it reduces entanglement between molecular chains, thereby decreasing tensile strength.
Table 1.
Changes in mechanical properties of HNBR over aging time in the thermal oil condition at 150 °C.
3.1.2. Aging Analysis of HNBR Vulcanized Rubber in a 150 °C Hot Water Environment
Table 2 shows the changes in the mechanical properties of HNBR vulcanized rubber after aging in a 150 °C hot water environment. From the table, it can be observed that the mechanical properties of HNBR vulcanized rubber also undergo some changes before and after aging. Specifically, the hardness increases with aging time, while the tensile strength experiences some loss. The elongation at break also shows a slight decrease. The variation rates in volume and mass are very small and can be considered negligible.
Table 2.
Changes in mechanical properties of HNBR over aging time in the 150 °C hot water condition.
3.1.3. Aging Analysis of HNBR Vulcanized Rubber in a 150 °C Hot Oxygen Environment
Table 3 presents the changes in the mechanical properties of HNBR vulcanized rubber before and after aging in a 150 °C thermo-oxidative environment. It can be observed that the mechanical properties of the vulcanizate undergo significant changes under thermo-oxidative conditions. The hardness increases continuously with aging time, while the tensile strength first increases and then decreases. The elongation at break shows a sharp decline with prolonged aging time. Based on these observations, it is inferred that crosslinking reactions occur in HNBR vulcanized rubber under thermo-oxidative conditions.
Table 3.
Changes in mechanical properties of HNBR over aging time in the 150 °C thermal oxygen condition.
3.1.4. Aging Analysis of HNBR Vulcanized Rubber in a 150 °C Oil–Water Mixed Environment
Table 4 presents the aging behavior of HNBR vulcanized rubber in a 150 °C oil–water mixed environment across different phases. It can be observed that the aging phenomena of HNBR differ significantly between the phases. In the oil phase, the vulcanized rubber experiences severe degradation in mechanical properties, along with considerable changes in volume and mass. In contrast, the mechanical properties of the vulcanized rubber in the water phase show minimal changes. Therefore, aging in the oil phase dominates the aging process of HNBR vulcanized rubber in the 150 °C oil–water environment.
Table 4.
Changes in mechanical properties of HNBR vulcanizate before and after aging in different phases in oil–water environment at 150 °C.
3.1.5. Aging Analysis of HNBR Vulcanized Rubber in a 150 °C Hot Oil (Oxygenated) Environment
Table 5 presents the aging behavior of HNBR vulcanized rubber in a 150 °C hot oil (oxidizing) environment. It can be observed that the rubber undergoes significant aging in this environment, with noticeable decreases in hardness, tensile strength, and elongation at break, as well as considerable changes in both volume and mass. In previous experiments, we found that under 150 °C conditions, the rubber’s hardness increased to a certain extent, with negligible changes in volume and mass. However, under hot oil (oxidizing) conditions, the hardness of the HNBR vulcanized rubber not only failed to increase but actually decreased significantly. Therefore, it can be concluded that in the 150 °C oil (oxidizing) environment, oil aging dominates the aging process of HNBR vulcanized rubber.
Table 5.
Changes in mechanical properties of HNBR over aging time in oil–oxygen environment at 150 °C.
3.1.6. Aging Analysis of HNBR Vulcanized Rubber in a 150 °C Hot Water (Oxygenated) Environment
Table 6 presents the aging behavior of HNBR vulcanized rubber in a 150 °C hot water (oxidizing) environment. It can be observed that as the aging time increases, the hardness of HNBR vulcanized rubber gradually increases, while the tensile strength slightly decreases. The elongation at break decreases significantly, and both volume and mass changes increase over time. This trend is very similar to the changes observed in the hot oxygen aging process. Therefore, it can be concluded that in the 150 °C hot water (oxidizing) environment, thermal oxidative aging dominates the aging process of HNBR vulcanized rubber.
Table 6.
Changes in mechanical properties of HNBR over aging time in water and oxygen environment at 150 °C.
3.2. FTIR Analysis (Fourier Transform Infrared Spectroscopy)
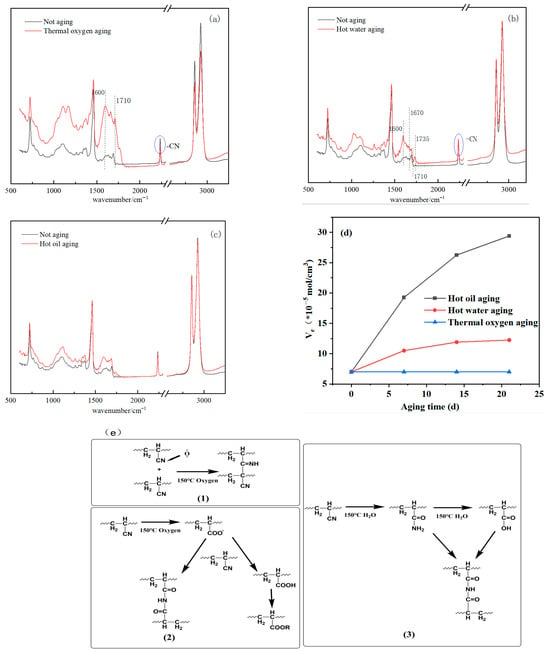
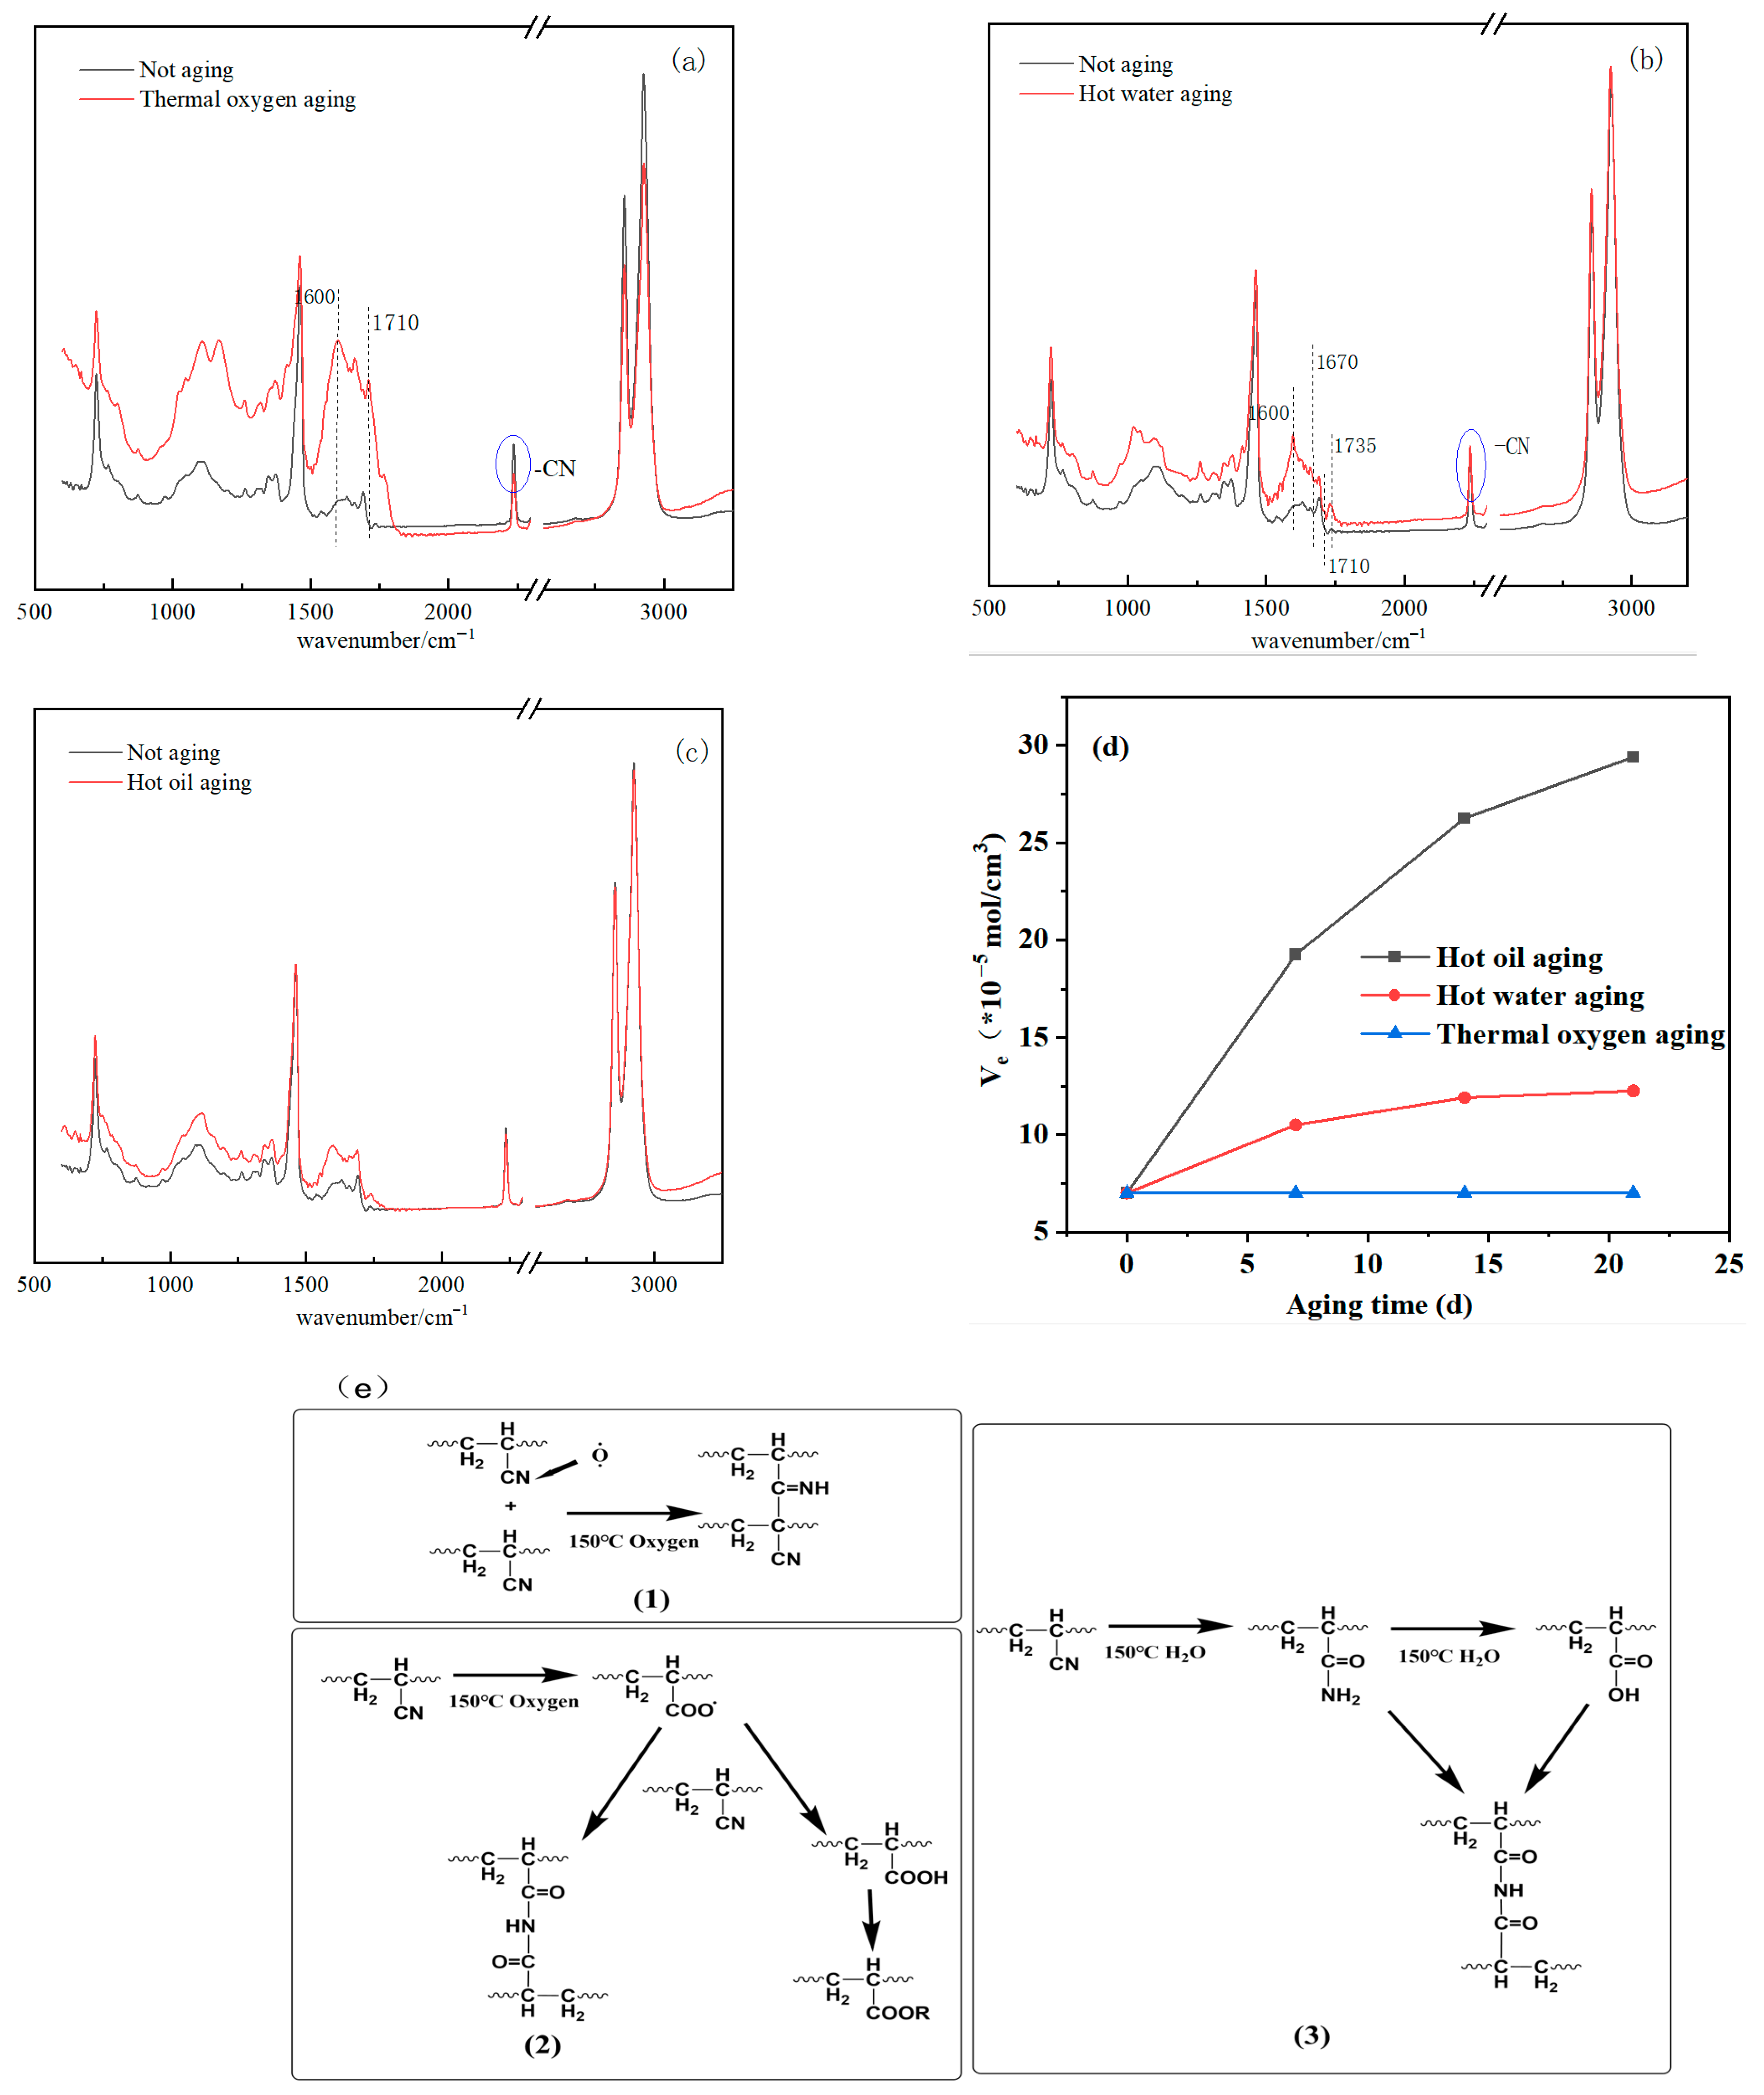
Figure 1 shows the infrared spectra of HNBR vulcanizates before and after aging in different environments. Specifically, Figure 1a,b present the ATR-FTIR results before and after aging under 150 °C thermo-oxidative and hot water conditions, respectively; Figure 1c displays the results under hot oil aging. The functional groups contained in HNBR are listed as follows: the absorption peak at 2237–2239 cm−1 is attributed to the C–N stretching vibration of the polyacrylonitrile (PAN) structural units in the polymer chain [30]. Since the structure undergoing aging cannot be observed, changes in molecular structure during the intermediate process can only be inferred. The infrared spectrum analysis is as follows:
Figure 1.
(a–c) ATR-FTIR spectra of HNBR vulcanizate before and after aging in different environments. (d) Changes in crosslinking density of HNBR vulcanizate before and after aging in different environments. (e1–e3) Aging mechanism of HNBR under hot oxygen and hot water.
Figure 1a,b correspond to the thermal oxidation aging and thermal water aging of HNBR vulcanized rubber, respectively. The intensity of the characteristic absorption peak of cyano groups (at 2235 cm−1) decreases, while the peak representing C=O (at 1710 cm−1) appears. Meanwhile, the peaks of imine bonds (-C=NH) at 1600 cm−1 and amide groups (R-CO-NH2) at 1627 cm−1 gradually become prominent. This indicates that a large number of carbonyl compounds are generated during the thermo-oxidative aging of HNBR vulcanizates [31,32].
Based on the above changes in the functional groups, it is inferred that the -CN groups in HNBR vulcanizates may undergo oxidation during aging under 150 °C thermo-oxidative and hot water conditions, generating groups such as carboxyl, ester, and amide groups. The corresponding mechanism is illustrated in Figure 1e [30,33]. For the aging of HNBR vulcanizates in the hot oil environment (Figure 1c), no significant changes are observed through comparison, suggesting that no obvious chemical changes occur. The loss of performance may be caused by changes in the microscopic morphology of the material.
3.3. Date Analysis of Crosslinking Density
The crosslinking density of the vulcanized rubber is represented by Ve (in units of 10−5 mol/cm3). Figure 1d illustrates the changes in the crosslinking density of HNBR vulcanized rubber before and after aging in different environments. It can be observed that under thermal oxidative conditions, the crosslinking density undergoes significant changes, continuously increasing over time. After 21 days of aging, the crosslinking density becomes more than four times the original value. Under hot water conditions, the crosslinking density also changes to a certain extent, and after 14 days of aging, it levels off, reaching approximately 1.6 times the original value. In contrast, under hot oil conditions, there is almost no change in the crosslinking density. This phenomenon can be attributed to the following mechanism: during the aging process, the α-H on the HNBR molecular chain is attacked by free radicals; acyl groups or amides are formed during aging. These processes induce excessive cross-linking reactions, leading to the formation of an overdeveloped cross-linking network, which ultimately results in a decrease in elongation at break.
3.4. Dynamic Mechanical Analysis (DMA)
Under the hot oil environment, the mechanical properties of HNBR vulcanizates decrease significantly; however, no obvious changes in the vulcanizates are observed via FTIR and cross-linking density tests. Therefore, it is hypothesized that under hot oil conditions, the slight chemical structure changes in HNBR allow oil to penetrate into the interior of the rubber. This penetration dissolves the rubber additives inside the rubber, leading to the formation of pores and swelling of the rubber. Additionally, the oil acts as a plasticizer in the rubber, which further reduces the mechanical properties of the rubber. Consequently, DMA tests were conducted on the HNBR vulcanizates before and after aging.
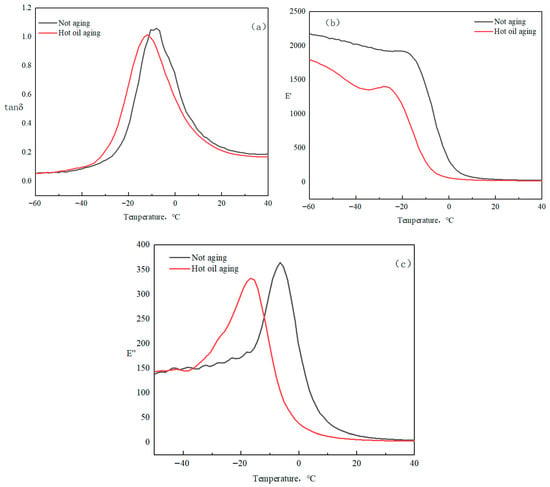
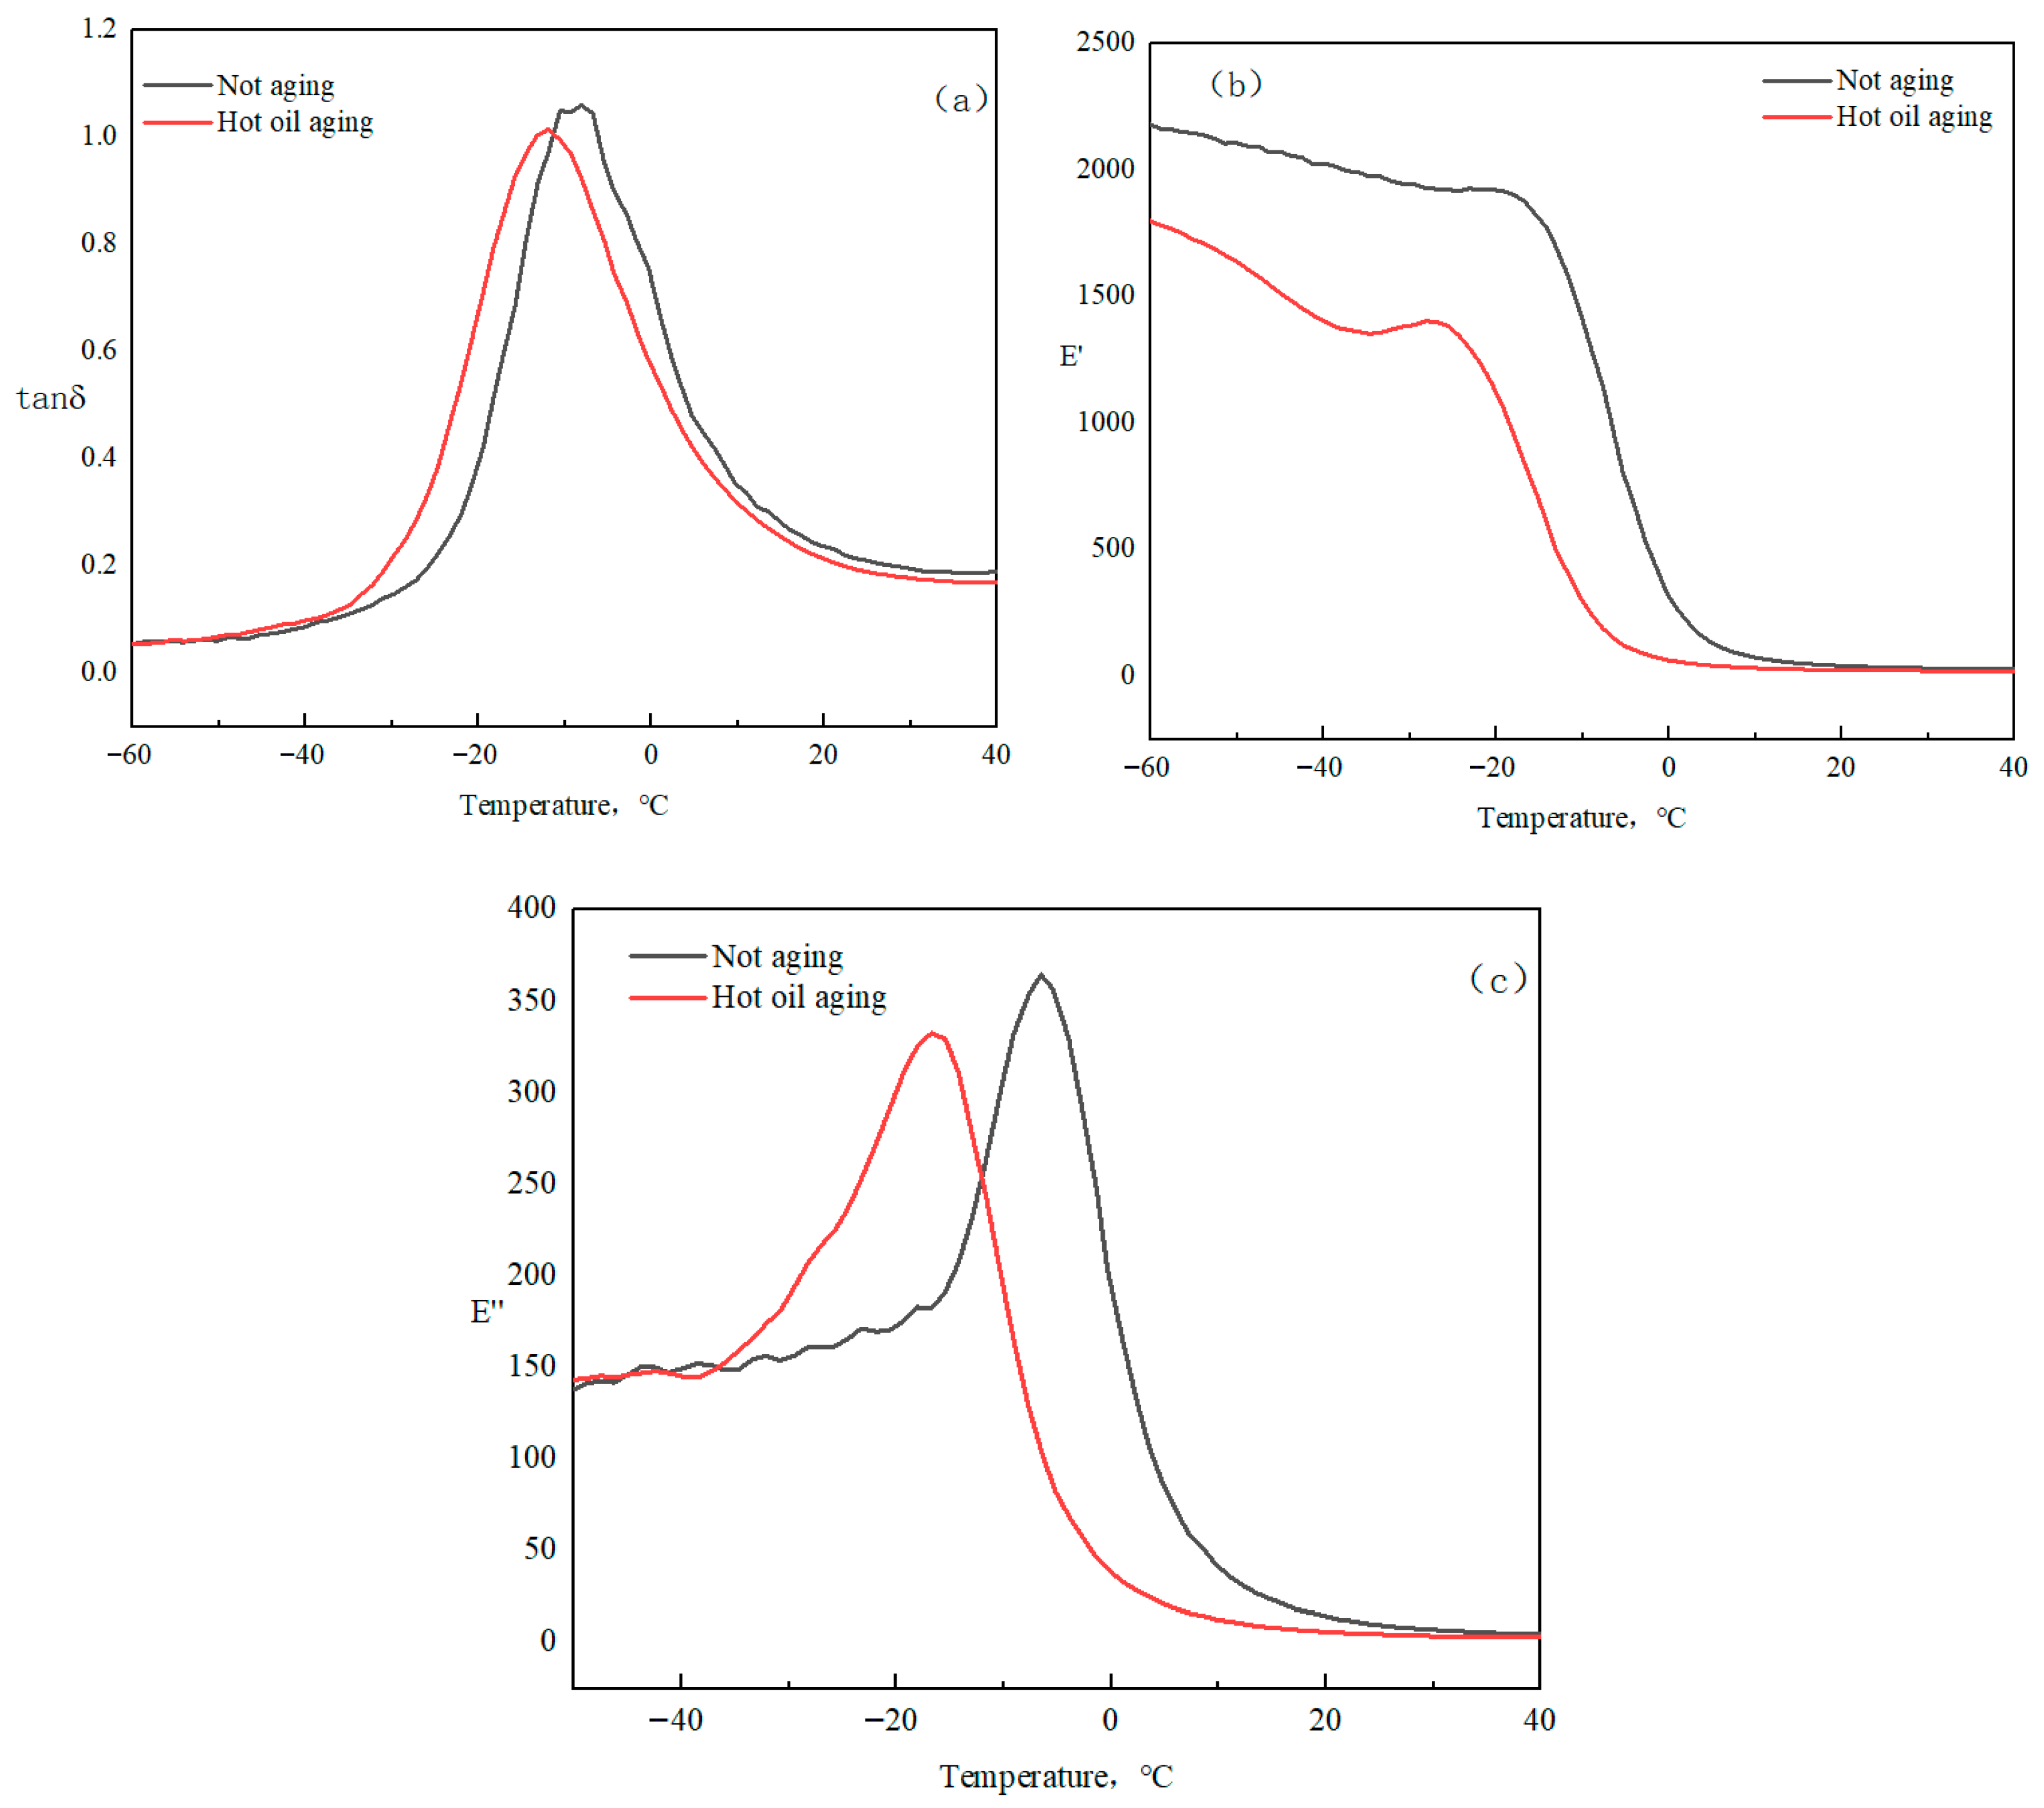
Figure 2 presents the DMA curves of HNBR vulcanizates before and after aging in a hot oil environment. As observed from the figures, after hot oil aging, the loss factor of the HNBR vulcanizates decreases, with a corresponding reduction in the glass transition temperature; meanwhile, the storage modulus and loss modulus also decrease to a certain extent. These results confirm our previous hypothesis: during the hot oil aging of HNBR vulcanizates, the slight chemical structure changes in HNBR allow oil to penetrate into the rubber interior, thereby exerting a plasticizing effect. A peak appears in Figure 2b, which may be attributed to the following mechanism: at low temperatures, small-molecule oils penetrating into the rubber matrix exhibit low solubility in the polar nitrile rubber molecules. These oils adsorb onto the surface of carbon black particles, thereby weakening the intermolecular forces between rubber chains and carbon black. When the temperature rises to −40 °C, the oil molecules dissolve into the rubber matrix, restoring the intermolecular forces between carbon black and rubber molecules, leading to an increase in modulus.
Figure 2.
DMA curve of HNBR vulcanizate before and after aging in hot oil environment. (a) Loss factor, (b) storage modulus, and (c) loss modulus of HNBR vulcanizate before and after aging in hot oil environment.
3.5. Scanning Electron Microscopy (SEM) Analysis
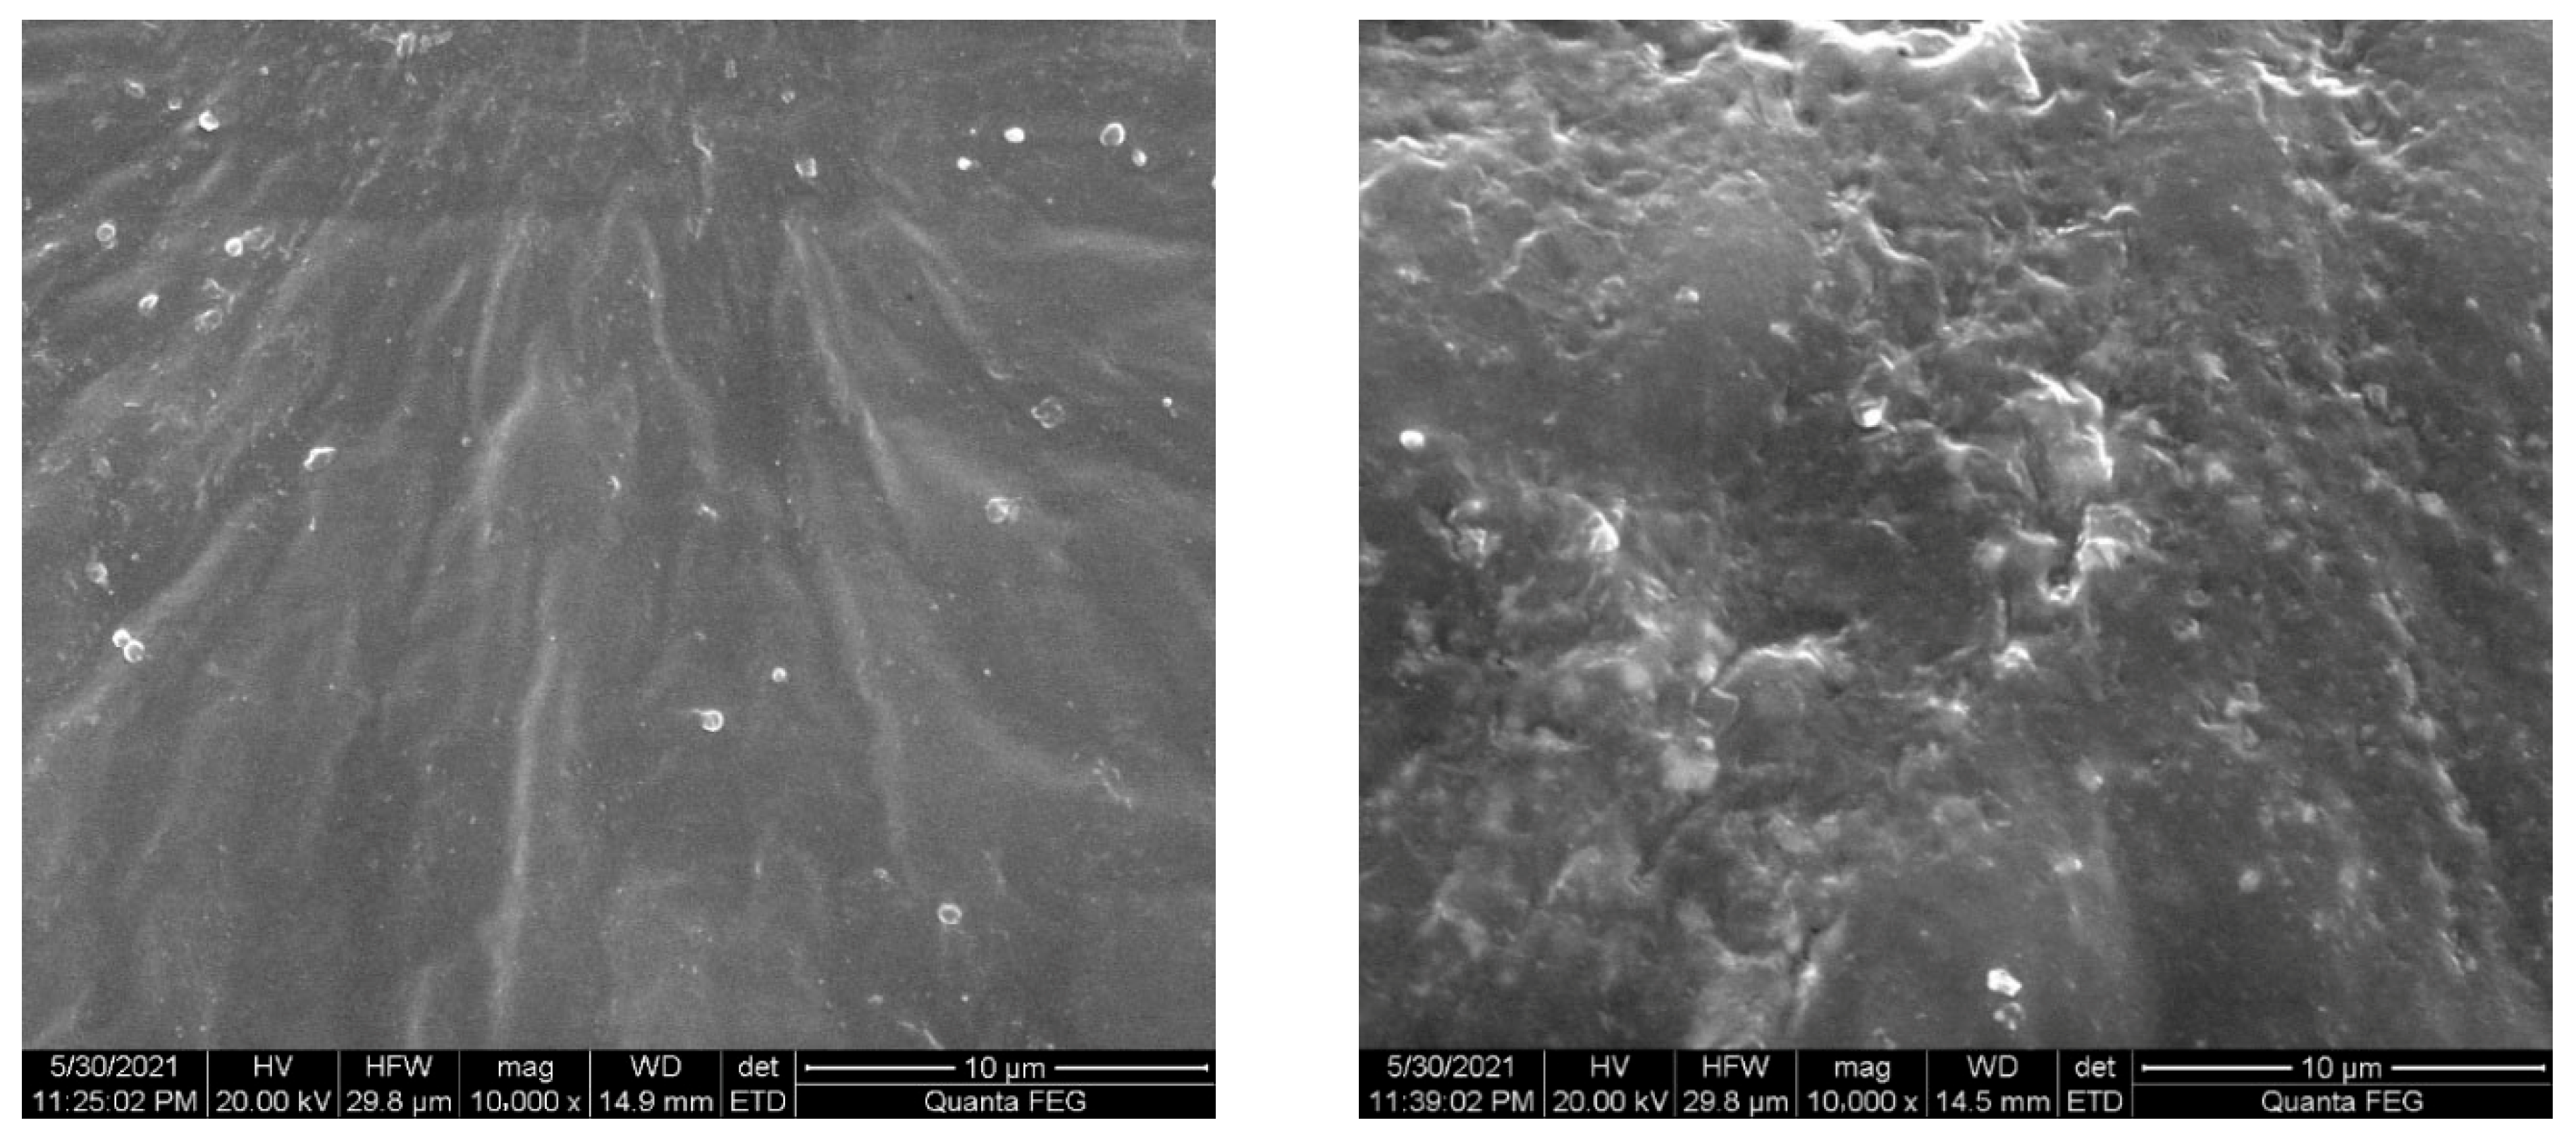
Figure 3 shows the scanning electron microscopy (SEM) images of the HNBR vulcanizate surface before and after aging in a hot oil environment, with the left image representing the state before aging and the right image showing the state after aging. It can be observed that the rubber surface undergoes significant changes after aging: the surface of the vulcanizate becomes rough and uneven, with the appearance of pore-like structures of varying sizes. These pore-like structures are exactly the channels through which the oil medium penetrates into the rubber interior, caused by the slight chemical structure changes in HNBR. SEM images showing aging in other media were not as pronounced as those in oil media and thus lacked reference value. Hence, they were not included in the literature.
Figure 3.
Surface SEM of HNBR vulcanizate before and after aging in hot oil environment.
4. Discussion
This study elucidates the distinct aging mechanisms of HNBR vulcanizates in high-temperature oil–water environments. The dominant aging pathway is critically dependent on the surrounding medium. In hot oil and oil–oxygen environments, physical swelling and plasticization induced by oil absorption are the predominant factors, leading to a significant decline in mechanical properties despite the presence of oxygen, which would typically cause hardening. This is because rapid oil penetration and its plasticizing effect overwhelm and suppress the oxidative crosslinking process. Conversely, in hot oxygen and water–oxygen environments, oxidative crosslinking dominates, resulting in hardening and embrittlement. These findings underscore the competitive nature of physical and chemical aging mechanisms in complex service environments, providing crucial insights for the future development of high-performance, aging-resistant HNBR materials.
5. Conclusions
Using HNBR vulcanized rubber as the base material, the aging behavior of HNBR vulcanized rubber in a 150 °C oil–water mixed medium was investigated. Independent environmental aging tests, as well as mixed environment aging tests, were conducted to explore the effects of different environments on the aging of HNBR vulcanized rubber. Finally, FTIR analysis, crosslink density analysis, DMA, and SEM were used to characterize the changes in HNBR vulcanized rubber during the aging process. The following conclusions were drawn:
- (1)
- HNBR vulcanized rubber exhibits different aging behaviors under different environments. In hot oxygen, hot water, and hot oxygen–water mixed environments, the rubber becomes harder, and the tensile strength decreases. However, aging is more pronounced under the hot oxygen and hot oxygen–water mixed conditions. In hot oil and mixed oxygen–oil environments, the rubber exhibits different aging behaviors, characterized by a decrease in hardness, as well as a significant reduction in tensile strength and elongation at break.
- (2)
- FTIR and crosslink density analyses reveal that under hot oxygen and hot water conditions, the vulcanized rubber undergoes some reactions, resulting in the formation of carbonyl compounds and an increase in crosslink density. In contrast, no significant changes occur in the hot oil environment. DMA and SEM analysis of the hot oil-aged samples show that in the oil medium, the oil penetrates into the rubber, causing swelling, and the oil acts as a plasticizer.
6. Future Work
This study proposes the aging mechanism of HNBR vulcanizates in high-temperature oil–water environments, but the anti-aging performance of HNBR vulcanizates has not been investigated in depth. In the future, the improvement of the anti-aging performance of HNBR vulcanizates under high-temperature oil–water conditions can be approached from aspects such as molecular structure optimization and formula design. Molecular structure optimization is the core, and it is necessary to further explore the enhancing effect of the introduction of special side chain groups on stability. Formula design should focus on efficient synergistic systems. A highly promising direction involves the development of immobilized macro-molecular anti-aging agents. By grafting or loading stabilizer molecules onto carrier substrates (e.g., nano-fillers or polymer microspheres), their migration and extraction in aggressive media can be significantly suppressed. This approach ensures a long-lasting protective effect within the rubber matrix, directly countering the swelling and plasticization degradation pathways identified in this study. Fu et al. [34] processed carbon nanotubes via ball milling to open their end caps, then employed acid etching for expansion, further enhancing their loading efficiency. Loading the anti-aging agent 4020 achieved a 30% loading efficiency. Subsequently, when incorporated as a nanofiller into styrene-butadiene rubber, it effectively improved the rubber’s resistance to thermal-oxidative aging while preventing blooming.
Improving the aging resistance of rubber materials also contributes to their recycling and reuse. Recycling and reutilization of materials have become an essential aspect of sustainable development today [35,36]. In the oil field, the use of rubber materials is substantial, including rubber hoses for oil and gas transportation, sealing rings, and the rubber cores in blowout preventers, all of which require significant amounts of rubber materials. Enhancing the aging resistance of these materials helps to reduce the frequency of rubber material recycling. Furthermore, improving the aging resistance also aids in minimizing the premature failure of rubber components, thereby extending the lifespan of related equipment and reducing the likelihood of early equipment retirement.
Supplementary Materials
The following supporting information can be downloaded at: https://www.mdpi.com/article/10.3390/coatings15121473/s1, Table S1. Formulation for HNBR preparation. Table S2. changes of mechanical properties of HNBR vulcanizates with different cyano content before and after aging.
Author Contributions
Conceptualization, J.L. and H.Y.; methodology, X.Z.; validation, J.C., T.X. and J.T.; formal analysis, J.C.; investigation, T.X.; resources, J.L.; data curation, J.T.; writing—original draft preparation, J.T.; writing—review and editing, H.Y.; supervision, J.L.; project administration, J.L.; funding acquisition, J.L. All authors have read and agreed to the published version of the manuscript.
Funding
This research received no external funding.
Institutional Review Board Statement
Not applicable.
Informed Consent Statement
Not applicable.
Data Availability Statement
Data is contained within the article or Supplementary Materials.
Conflicts of Interest
Authors Junan Lu, Xuliang Zhang, Jianglin Chen, Tianguo Xia were employed by Petrochina Tarim Oilfield Company. The remaining authors declare that the research was conducted in the absence of any commercial or financial relationships that could be construed as a potential conflict of interest.
References
- Chung, E.; Kittur, M.; Andriyana, A.; Ganesan, P. On the thermo-oxidative aging of elastomers: A comprehensive review. Polymer 2024, 304, 127109. [Google Scholar] [CrossRef] [Scilit]
- Hassani, F.; Faisal, N.H.; Nish, R.; Rothnie, S.; Njuguna, J. The impact of thermal ageing on sealing performance of HNBR packing elements in downhole installations in oilfield wellhead applications. J. Pet. Sci. Eng. 2022, 208, 109200. [Google Scholar] [CrossRef] [Scilit]
- Qiao, Z.; Guo, Y.; Zhang, Z.; Wang, X.; Wang, D. Fretting behavior of hydrogenated nitrile rubber for sealing application of ultra-deep well. Tribol. Int. 2025, 202, 110328. [Google Scholar] [CrossRef] [Scilit]
- Chen, X.; Zonoz, R.H.; Salem, H.A.; Lim, H.K. Extrusion resistance and high-pressure sealing performance of hydrogenated nitrile-butadiene rubber (HNBR). Polym. Test. 2019, 76, 499–504. [Google Scholar] [CrossRef] [Scilit]
- Balasooriya, W.; Schrittesser, B.; Wang, C.; Hausberger, A.; Pinter, G.; Schwarz, T. Tribological Behavior of HNBR in Oil and Gas Field Applications. Lubricants 2018, 6, 20. [Google Scholar] [CrossRef] [Scilit]
- Cong, C.; Liu, Q.; Li, J.; Meng, X.; Zhou, Q. Synergistic crosslink of double bond and nitrile group of nitrile rubber in H2S environment. Polym. Degrad. Stab. 2018, 157, 108–118. [Google Scholar] [CrossRef] [Scilit]
- Li, S.; Wu, X.; Liu, H.; Wang, H.; Li, Z. Dual-fillers synergistic strategy for highly efficient anti-aging HNBR composite. Compos. Sci. Technol. 2025, 271, 111342. [Google Scholar] [CrossRef] [Scilit]
- Kömmling, A.; Jaunich, M.; Pourmand, P.; Wolff, D.; Hedenqvist, M. Analysis of O-Ring Seal Failure under Static Conditions and Determination of End-of-Lifetime Criterion. Polymers 2019, 11, 1251. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Ilseng, A.; Skallerud, B.H.; Clausen, A.H. Tension behaviour of HNBR and FKM elastomers for a wide range of temperatures. Polym. Test. 2016, 49, 128–136. [Google Scholar] [CrossRef] [Scilit]
- Khelidj, N.; Colin, X.; Audouin, L.; Verdu, J.; Monchy-Leroy, C.; Prunier, V. Oxidation of polyethylene under irradiation at low temperature and low dose rate. Part II. Low temperature thermal oxidation. Polym. Degrad. Stab. 2006, 91, 1598–1605. [Google Scholar] [CrossRef] [Scilit]
- Alcock, B.; Jørgensen, J.K. The mechanical properties of a model hydrogenated nitrile butadiene rubber (HNBR) following simulated sweet oil exposure at elevated temperature and pressure. Polym. Test. 2015, 46, 50–58. [Google Scholar] [CrossRef] [Scilit]
- Alcock, B.; Peters, T.A.; Gaarder, R.H.; Jørgensen, J.K. The effect of hydrocarbon ageing on the mechanical properties, apparent crosslink density and CO2 diffusion of a hydrogenated nitrile butadiene rubber (HNBR). Polym. Test. 2015, 47, 22–29. [Google Scholar] [CrossRef] [Scilit]
- Hertz, D.L.; Bussem, H.; Ray, T.W. Nitrile Rubber—Past, Present and Future. Rubber Chem. Technol. 1995, 68, 540–546. [Google Scholar] [CrossRef] [Scilit]
- Zeng, D.; Dong, B.; Qi, Y.; Yu, Z.; Wang, J.; Huang, X.; Liu, X.; Liu, Y. On how CO2 partial pressure on corrosion of HNBR rubber O-ring in CO2–H2S–CH4 environment. Int. J. Hydrogen Energy 2021, 46, 8300–8316. [Google Scholar] [CrossRef] [Scilit]
- Smejda-Krzewicka, A.; Mrozowski, K.; Strzelec, K. Interelastomer Reactions Occurring during the Cross-Linking of Hydrogenated Acrylonitrile-Butadiene (HNBR) and Chloroprene (CR) Rubbers Blends in the Presence of Silver(I) Oxide (Ag2O) and Mechanical Properties of Cured Products. Materials 2023, 16, 4573. [Google Scholar] [CrossRef] [Scilit]
- Budrugeac, P. Thermooxidative degradation of some nitrile-butadiene rubbers. Polym. Degrad. Stab. 1992, 38, 165–172. [Google Scholar] [CrossRef] [Scilit]
- Verdier, N.; Lepage, D.; Prébé, A.; Aymé-Perrot, D.; Dollé, M.; Rochefort, D. Crosslinker free thermally induced crosslinking of hydrogenated nitrile butadiene rubber. J. Polym. Sci. 2018, 56, 1825–1833. [Google Scholar] [CrossRef] [Scilit]
- Schurz, J. Discoloration effects in acrylonitrile polymers. J. Polym. Sci. 1958, 28, 438–439. [Google Scholar] [CrossRef] [Scilit]
- Wang, H.; Yang, L.; Rempel, G.L. Homogeneous hydrogenation art of nitrile butadiene rubber: A review. Polym. Rev. 2013, 53, 192–239. [Google Scholar] [CrossRef] [Scilit]
- Giurginca, M.; Zaharescu, T. Thermo-oxidative degradation of some polymer couples containing HNBR. Polym. Bull. 2003, 49, 357–362. [Google Scholar] [CrossRef] [Scilit]
- Mengistu, T.; Pazur, R.J. The thermal oxidation of hydrogenated acrylonitrile-co-butadiene rubber from ambient to 150 °C. Polym. Degrad. Stab. 2021, 188, 109574. [Google Scholar] [CrossRef] [Scilit]
- Wang, Z.; Su, M.; Li, X.; Ma, C.; Hu, F.; Miao, Z.; Song, J.; Ma, L.; Li, W. Effect of carboxyl group introduction and graft modification on the thermal properties and Fe wall adsorption performance of HNBR. Comput. Mater. Sci. 2024, 231, 112592. [Google Scholar] [CrossRef] [Scilit]
- Akulichev, A.G.; Alcock, B.; Krauklis, A.E.; Tiwari, A.; Echtermeyer, A.T. Long-term ISO 23936-2 sweet oil ageing of HNBR. Polym. Test. 2021, 102, 107343. [Google Scholar] [CrossRef] [Scilit]
- Longo, A.; Palomba, M.; Giubileo, F.; Carotenuto, G. Contrast enhancement in 2D nanomaterial SEM images. Eng. Proc. 2025, 87, 81. [Google Scholar]
- GB/T 531.1-2008; Rubber, Vulcanized or Thermoplastic—Determination of Indentation Hardness—Part 1: Durometer Method. Standards Press of China: Beijing, China, 2008.
- GB/T 528-2009; Rubber, Vulcanized or Thermoplastic—Determination of Tensile Stress-Strain Properties. Standards Press of China: Beijing, China, 2009.
- Rodriguez, F.; Cohen, C.; Ober, C.K.; Archer, L. Principles of Polymer Systems; CRC Press: Boca Raton, FL, USA, 2014. [Google Scholar]
- Kraus, G. Swelling of filler-reinforced vulcanizates. J. Appl. Polym. Sci. 1963, 7, 861–871. [Google Scholar] [CrossRef] [Scilit]
- Guo, B.; Lei, Y.; Chen, F.; Liu, X.; Du, M.; Jia, D. Styrene–butadiene rubber/halloysite nanotubes nanocomposites modified by methacrylic acid. Appl. Surf. Sci. 2008, 255, 2715–2722. [Google Scholar] [CrossRef] [Scilit]
- Tan, J.; Chen, C.; Wu, J.; He, R.; Jiang, L.; Liu, Y. Influence of ultraviolet aging on the structure, mechanical and gas permeability properties of hydrogenated nitrile butadiene rubber. J. Appl. Polym. Sci. 2021, 138, 50543. [Google Scholar] [CrossRef] [Scilit]
- Zhang, Z.; Li, H.; Zhou, H.; Zhao, L.; Li, S.; Wang, H.; Wang, Z.; Li, Z. Modification and improvement of aging resistance for HNBR/graphite composites. J. Macromol. Sci. Part A 2022, 59, 285–294. [Google Scholar] [CrossRef] [Scilit]
- Lou, W.; Zhang, W.; Jin, T.; Liu, X.; Wang, H. Stress–thermal oxidative aging behavior of hydrogenated nitrile rubber seals. J. Appl. Polym. Sci. 2019, 136, 47014. [Google Scholar] [CrossRef] [Scilit]
- Li, S.; Zhou, H.; Zheng, F.; Du, Z.; Cai, R.; Li, D.; Zhang, Z.; Wang, H.; Li, Z. Investigation of the properties and aging mechanisms of vulcanized hydrogenated nitrile rubber in different mediums. Polym. Adv. Technol. 2022, 34, 928–938. [Google Scholar] [CrossRef] [Scilit]
- Fu, Y.; Yang, C.; Lvov, Y.M.; Zhang, L.; Wang, W. Antioxidant sustained release from carbon nanotubes for preparation of highly aging resistant rubber. Chem. Eng. J. 2017, 328, 536–545. [Google Scholar] [CrossRef] [Scilit]
- Yıldız, T.D. Considering the development levels of countries, contributions of mineral recovery from mining tailings and urban mining wastes to sustainability criteria—A review. Resour. Policy 2024, 99, 105399. [Google Scholar] [CrossRef] [Scilit]
- Du, Y.; Ju, T.; Meng, Y.; Han, S.; Jiang, J. Pyrolysis characteristics of excavated waste and generation mechanism of gas products. J. Clean. Prod. 2022, 370, 133489. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2025 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license (https://creativecommons.org/licenses/by/4.0/).