


Abstract
To develop novel biodegradable magnesium alloys with suitable corrosion resistance and mechanical properties for orthopedic applications, this study investigated the microstructure, mechanical properties, corrosion behavior and wear resistance of as-cast and near-solidus heat-treated Mg-3Zn-0.3Mn alloys with and without Gd/Nd additions (RE-free, 1Gd, 1Gd1Nd). Rare earth addition refined the grains and transformed the secondary phase from Mg7Zn3 to the W-phase (Mg3RE2Zn3). The as-cast 1Gd1Nd alloy showed the finest grains, highest hardness (51.3 HB), best tensile strength (189.38 MPa), lowest corrosion rate (2.80 mm/y) and lowest wear rate (0.614 × 10⁻³ mm3/(N·m)). Near-solidus heat treatment slightly decreased hardness (1–3%) but significantly reduced corrosion rate (e.g., RE-free alloy from 3.61 to 2.78 mm/y) and wear rate. The heat-treated 1Gd1Nd alloy gave the best overall performance: corrosion rate 2.68 mm/y, tensile strength 213.71 MPa and elongation 12.96%. Gd promoted grain refinement and film stability, while Nd stabilized the W-phase, showing a clear combined addition benefit. Notably, the heat-treated RE-free alloy performed similarly to the as-cast 1Gd1Nd alloy, indicating that heat treatment can partially mimic rare earth addition. This work provides a baseline for precursor materials before further processing (e.g., extrusion) toward biodegradable implant applications.
1. Introduction
Magnesium alloys are considered a highly promising new generation of biomedical metallic materials owing to their biodegradability, excellent biocompatibility, and bone-like mechanical properties [1,2,3]. They hold significant potential for applications in orthopedic implants and cardiovascular stents. However, a major obstacle to their clinical adoption is their excessively rapid and often non-uniform corrosion and degradation in physiological environments [4,5]. This can lead to premature mechanical failure of the implant before bone healing is complete, as well as complications arising from localized hydrogen accumulation, which severely limits their clinical translation [6,7]. Therefore, controlling the degradation rate while maintaining adequate mechanical support throughout the service period remains a central challenge in the development of clinically viable biodegradable magnesium alloys [8,9,10].
Among various biocompatible alloy systems, Mg–Zn alloys have garnered considerable interest because of the physiological essentiality of zinc (Zn) in the human body and its solid-solution strengthening effect [11,12,13]. However, conventionally cast high-zinc (>3 wt.%) Mg–Zn alloys often exhibit coarse grains and a continuous network of Mg7Zn3 phases along grain boundaries, which lead to inadequate mechanical performance and pronounced galvanic corrosion. To address these issues, the addition of trace amounts of manganese (Mn) has emerged as an effective strategy [14]. Mn not only refines the grain structure through the formation of fine particles but also enhances alloy purity by “fixing” detrimental impurity elements such as iron (Fe) [15]. Furthermore, Mn promotes the formation of a more stable and protective surface layer of corrosion products (e.g., Mn-containing oxides/hydroxides), thereby significantly improving corrosion resistance [16]. Previous studies have confirmed that incorporating Mn into Mg–Zn alloys effectively slows their degradation both in vitro and in vivo [16,17,18].
The addition of rare earth (RE) elements, such as yttrium (Y) and neodymium (Nd), is regarded as a key strategy for co-additionally improving the overall performance of magnesium alloys [19,20,21,22]. RE elements can substantially enhance the strength, ductility, and creep resistance of alloys through strong solid-solution strengthening and the formation of fine, thermally stable Mg-RE-Zn intermetallic compounds (e.g., long-period stacking ordered, LPSO, phases) [23,24,25]. Simultaneously, RE elements modify the structure and composition of corrosion products, promoting the formation of a denser and more adherent protective surface film, thereby encouraging a more uniform corrosion mode. It should be noted, however, that the beneficial effects of RE elements strongly depend on their specific existence forms and spatial distribution within the microstructure, which are directly governed by the alloy’s preparation and processing routes [26,27].
For biomedical magnesium alloys, the rare earth (RE) content should be kept as low as possible to minimize potential long-term biological risks. Our previous studies on Gd-modified magnesium alloys [28] clearly demonstrated that increasing the Gd content beyond 1 wt.% does not further improve mechanical or corrosion properties; in some cases, properties even deteriorate. Therefore, 1 wt.% was selected as an appropriate addition level for both Gd and Nd. This concentration also lies close to the solid solubility limit of Nd in Mg (about 0.6 wt.%), which helps maximize solid-solution strengthening while avoiding the formation of excessive coarse secondary phases. In Mg–Zn–Mn and similar wrought Mg alloys, an RE addition of approximately 1 wt.% is often considered an optimal window for achieving grain refinement, texture weakening, and a desirable strength–ductility balance; lower additions give insufficient modification, whereas higher levels tend to promote brittle phases, impair toughness, and may accelerate galvanic corrosion.
Conventional casting tends to induce compositional segregation and coarse secondary phases, which limits the scope for optimizing material properties. In contrast, solid-solution heat treatment—as a controlled processing route—promotes spheroidization and refinement of primary α-Mg grains within the solid-solution temperature range and enables uniform, dispersed distribution of eutectic structures [29,30,31,32]. This offers a pathway to fundamentally improve the alloy’s microstructure and overall performance. The temperature and duration of this process precisely regulate the solid fraction, grain morphology, and the dissolution and precipitation kinetics of secondary phases in the solid-solution state, which are key to determining the final microstructural characteristics. Although studies have separately examined the beneficial effects of rare-earth alloying or solid-solution processing on magnesium alloys, there remains a lack of in-depth investigation into how solid-solution heat treatment, specifically applied to the Mg–Zn–Mn–RE multi-component alloy system, drives the co-addition evolution of “microstructure—mechanical properties—corrosion behavior.” Moreover, the ways in which this process precisely controls the morphology, size, and distribution of RE-containing secondary phases, and thereby influences the degradation mechanisms and mechanical longevity of the alloy in physiological environments, are still important scientific questions that need to be clarified.
Building upon this foundation, the present study employs a Mg–Zn–Mn alloy as the matrix, incorporates rare-earth elements (Gd and Nd), and co-addition applies solid-solution heat treatment. The objectives are to elucidate the influence of heat-treatment on the microstructural evolution of the alloy and to evaluate their effects on mechanical properties and corrosion behavior in simulated body fluid. This research aims to establish the intrinsic relationship among “process parameters—microstructure—performance (mechanical/corrosion)”, thereby providing a new theoretical basis and experimental foundation for developing high-performance biodegradable Mg–Zn–Mn–RE alloys through process innovation. Moreover, the present study is a precursor work for our recently published research on hot-extruded Mg–Zn–Mn–(Gd,Nd) alloys. The same alloy compositions were used in both studies. The aim here is to systematically investigate the microstructural evolution from the as-cast to the heat-treated state before severe plastic deformation, which is essential for understanding the microstructure-property relationships in the final extruded materials. Hence, the choice of REs, concentration, and combination was motivated by both biomedical safety considerations and the need for consistency with our ongoing processing research.
2. Materials and Methods
2.1. Alloy Preparation
Mg-3Zn-0.3Mn (wt.%) alloy was used as the base material. Three alloys were prepared: the base alloy, an alloy with 1 wt.% Gd, and an alloy with 1 wt.% Gd + 1 wt.% Nd. The raw materials included pure Mg, pure Zn, manganese chloride, Mg-30 wt.% Gd, and Mg-30 wt.% Nd.
Before melting, the surface oxide layer of each raw material was removed by polishing. The materials were then dried in an electric blast oven at 60 °C for 2 h to eliminate surface moisture. After drying, the raw materials were placed in a crucible, and the temperature was gradually raised to 675 °C under a protective atmosphere of Ar2 + 1% SF6. Once the alloy was fully melted, it was mechanically stirred under argon for 15 min to ensure a uniform composition, followed by a 30 min holding period.
The melt was then poured under the protective atmosphere into a water-cooled aluminum alloy mold using a funnel. The temperature of hopper was 646 °C. This process produced an ingot with dimensions of Φ100 mm × 200 mm. The actual chemical compositions of the samples were determined by inductively coupled plasma atomic emission spectroscopy (ICP-AES, ICP6300, Thermo Fisher, Waltham, MA, USA), and the results are listed in Table 1.
Table 1.
The actual composition of experimental alloy.
2.2. Solid-Solution Heat Treatment
Differential scanning calorimetry (DSC) was performed on the as-cast Mg-3Zn-0.3Mn alloy using a DSC822 instrument (METTLER TOLEDO, Columbus, OH, USA). Two endothermic peaks were observed at 458 °C and 610 °C, corresponding to the dissolution of the Mg–Zn phase and the α-Mg matrix, respectively. Based on the result, a heat treatment temperature of 460 °C and a holding time of 12 h were selected. After heat treatment, the samples were cooled in air.
2.3. Preparation of Metallographic Specimens
Metallographic specimens were cut from the ingots using wire cutting and slicing tools. The specimens were then ground successively with 800, 1000, 2000, and 4000 grit SiC abrasive papers. Subsequently, they were polished using a flocked cloth and a red velvet cloth with 0.5 μm alumina polishing suspension.
For microstructural observation, the etching solution was prepared by diluting 2 mL of 10% oxalic acid standard solution with 98 mL of distilled water. Specimens were immersed in this solution for 5 s. After etching, the specimens were rinsed with alcohol and dried. The etched samples were then examined using an optical microscope and a scanning electron microscope (SEM). Grain sizes were measured using Nano Measurer 1.2 software.
2.4. Microstructure Analysis
Crystalline phases were identified by X-ray diffraction (XRD; D8 FORCUS, Bruker, Manning Park Billerica, MA, USA), using Cu Kα radiation (λ = 1.5406 Å), operated at 40 kV and 40 mA. Scans were performed for the 2θ range of 20–100° at a rate of 4°/min, with a step size of 0.02°.
Microstructure, fracture surfaces, and corrosion morphologies were examined by scanning electron microscopy (SEM; SU5000, Hitachi, Japan), operated at 15 kV with a working distance of 8–10 mm. Energy-dispersive X-ray spectroscopy (EDS) was employed for qualitative elemental analysis.
The elemental surface distribution was determined by electron probe microanalysis (EPMA; JXA-8530F PLUS, JEOL, Tokyo, Japan).
2.5. Microhardness Testing
Brinell hardness of the alloys was measured using a hardness tester (HBE-3000A, Beijing Time, Beijing, China). A tungsten carbide indenter with a diameter of 10 mm was used. The applied load was 1000 kgf, and the dwell time was 30 s. For each sample, at least five measurements were taken, and the average value was calculated to ensure accuracy.
2.6. Tensile Testing
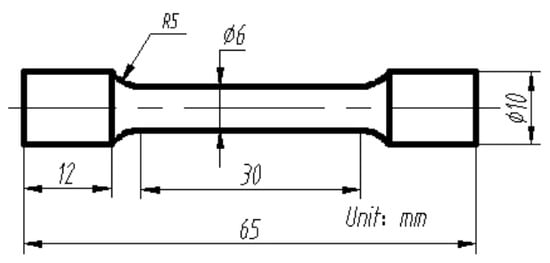
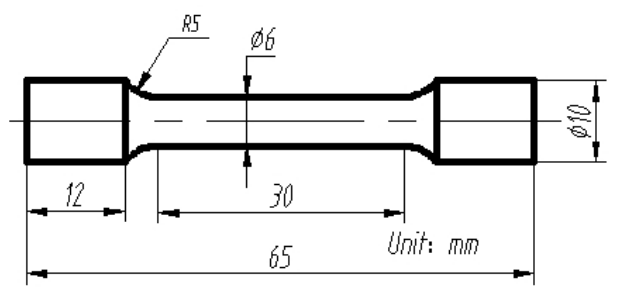
Room-temperature tensile tests were performed on a DNS-100 (Sinotest, Changchun, China) universal testing machine. A schematic drawing of the tensile specimen geometry is shown in Figure 1. Each alloy condition was tested using three specimens under the same conditions, and the average values were calculated to ensure data reliability.
Figure 1.
Dimensions of the tensile samples.
2.7. Wear Testing
Dry sliding wear tests were conducted using an MFT-1000T tribometer (Mega instruments, Suzhou, China). The samples were machined into pins with a height of 12.8 mm and a diameter of 4.8 mm. The counter disc was made of 304 stainless steel. The applied load was 50 N, the rotational speed was 100 r/min, the friction radius was 10 mm, and the test duration was 30 min.
Before and after each test, the height and diameter of the pins were measured using a vernier caliper. The wear volume was calculated from these measurements, and the wear rate was subsequently determined.
Friction coefficient:
In the formula, M is the friction torque obtained on the friction and wear tester, the radius of the wear track R = 10 mm, and N is the applied load (50 N).
Wear amount:
Sliding distance:
Wear rate:
In the formula, ∆H is the height difference before and after wear, d is the rotation radius of the pin specimen, ω is the rotational speed, t is the experimental time, F is the test load, and the unit of is mm3/(N·m).
2.8. Corrosion Properties Testing
Electrochemical tests were performed using a standard three-electrode system. An Ag/AgCl electrode (filled with saturated KCl) served as the reference, a Pt plate as the counter electrode, and the magnesium alloy sample as the working electrode.
Working electrodes were prepared as follows. Magnesium alloy samples (10 mm × 10 mm × 3 mm) were first welded to copper wires. The welded joints and the four sides of each sample were then cold-mounted in epoxy resin, leaving only the front face exposed to the electrolyte. The exposed area was kept as consistent as possible across all samples.
The test solution was Hank’s balanced salt solution at 37 ± 0.5 °C. Its chemical composition is given in Table 2. Before each measurement, the open-circuit potential (OCP) was recorded for 600 s until a stable value was reached. Electrochemical impedance spectroscopy (EIS) was then performed with an amplitude of 5 mV over a frequency range from 100 kHz to 0.01 Hz. Subsequently, potentiodynamic polarization curves were measured by scanning from −300 mV to +300 mV relative to the OCP at a scan rate of 1 mV/s. The EIS data were fitted to an equivalent circuit using ZSimpWin V3.60 software.
Table 2.
Chemical composition of Hank’s solution (g/L).
3. Results
3.1. Microstructure
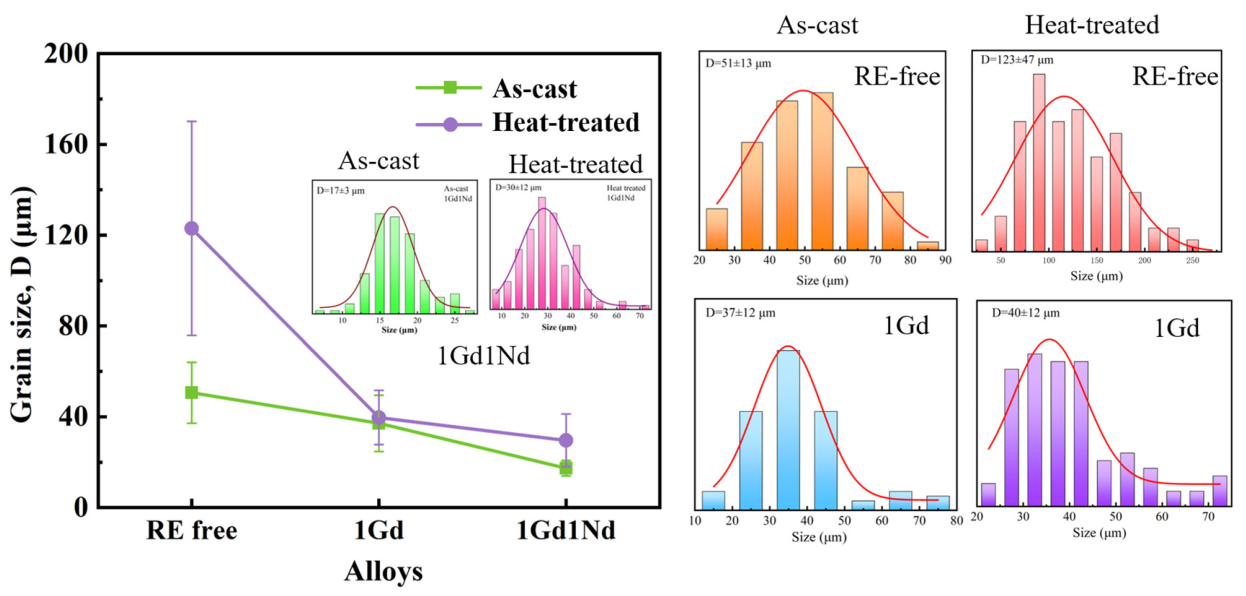
Figure 2 presents the grain size statistics of as-cast and heat-treated Mg-3Zn-0.3Mn (RE-free), Mg-3Zn-0.3Mn-1Gd (1Gd), and Mg-3Zn-0.3Mn-1Gd-1Nd (1Gd1Nd) samples. The as-cast RE-free alloy showed an average grain size of 51 ± 13 μm. With the addition of Gd, the grain size decreased to 37 ± 12 μm, and the secondary phase became more distinct. When Nd was added together with Gd, the grain size further decreased to 17 ± 3 μm. In this alloy, the number and volume fraction of the secondary phase increased, and the phase exhibited a continuous distribution. After heat treatment, the average grain sizes of all samples increased. The grain sizes of the RE-free, 1Gd, and 1Gd1Nd alloys were 123 ± 47 μm, 40 ± 12 μm, and 30 ± 12 μm, respectively.
Figure 2.
Grain size statistics of as-cast and heat-treated RE-free, 1Gd and 1Gd1Nd samples.
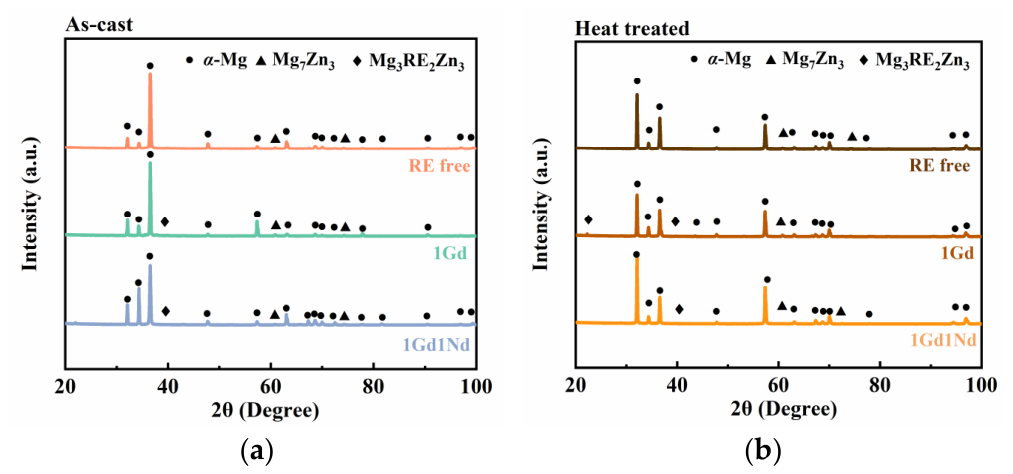
Figure 3 shows the XRD patterns of the as-cast and heat-treated RE-free, 1Gd, and 1Gd1Nd samples. In all alloys, the main phase was α-Mg, consistent with the high Mg content. In the as-cast RE-free alloy, the Mg7Zn3 phase was detected. With the addition of 1 wt.% Gd, the W-phase (Mg3RE2Zn3) appeared. When both Gd and Nd were added (1 wt.% each), the diffraction peaks of the W-phase became stronger and broader, indicating an increase in its volume fraction. After heat treatment, the Mg7Zn3 peaks in the RE-free alloy almost disappeared. The rare-earth-containing alloys still mainly consisted of α-Mg and the W-phase. However, the peak intensities of the W-phase were lower than those in the as-cast condition, suggesting that heat treatment caused partial dissolution of the rare-earth-rich phases and decomposed most of the Mg-Zn phases. No new phases were formed. Although Mn (0.3 wt.%) was present in all alloys, no Mn-containing phases were detected by XRD, likely because the Mn content was below the detection limit of the instrument.
Figure 3.
XRD results of as-cast (a) and heat-treated (b) RE-free, 1Gd and 1Gd1Nd samples.
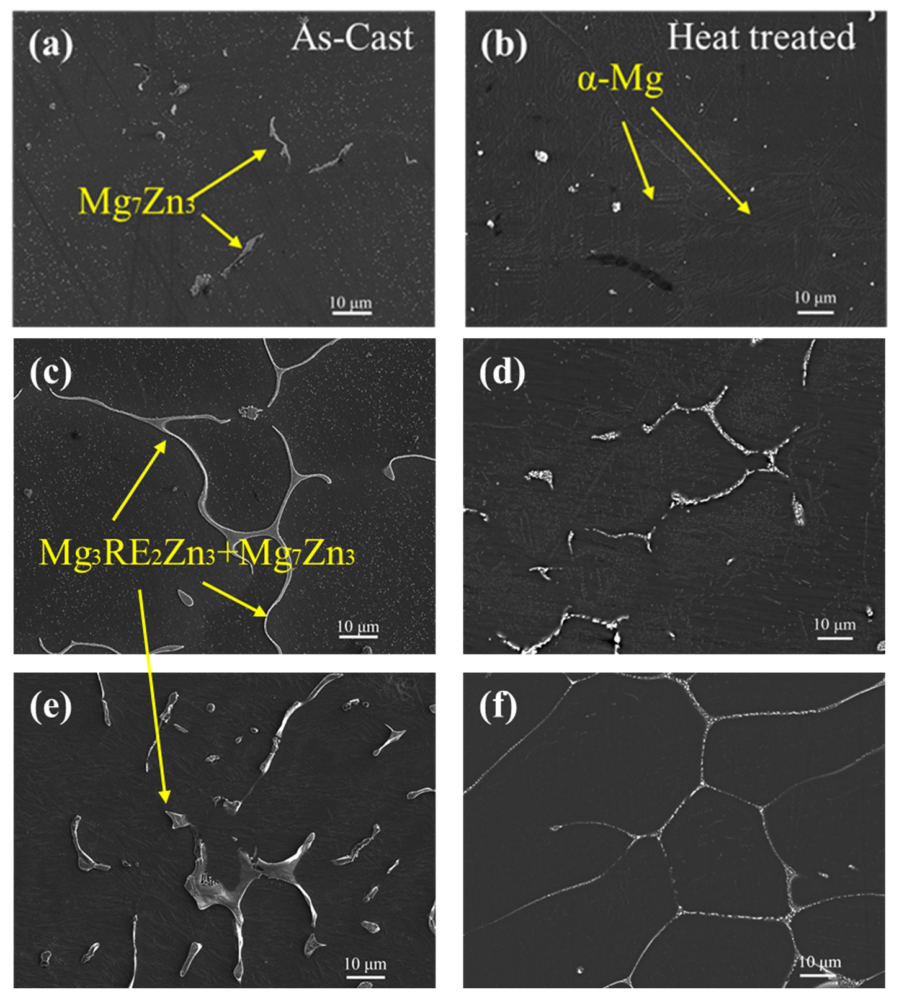
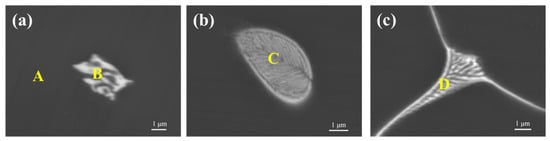
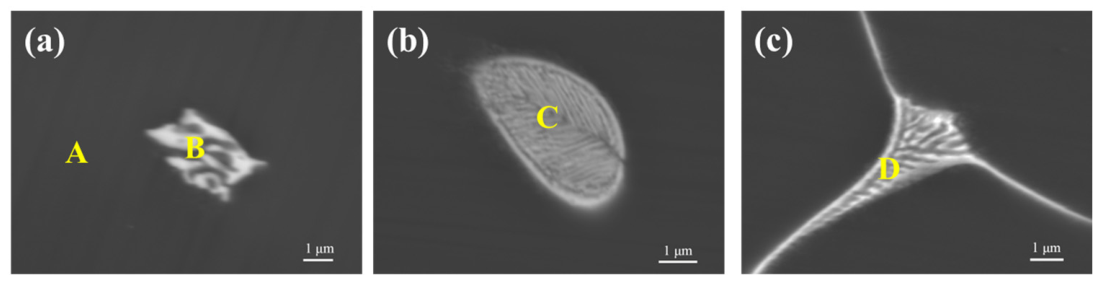
Figure 4 shows SEM micrographs of the as-cast and heat-treated RE-free, 1Gd and 1Gd1Nd samples. Figure 5 presents EPMA point-scan images of the as-cast samples, and the corresponding compositions are listed in Table 3.
Figure 4.
SEM microphotographics of as-cast (a,c,e) and heat-treated (b,d,f) RE-free (a,b), 1Gd (c,d) and 1Gd1Nd (e,f) samples.
Figure 5.
EMPA point-scanning images of as-cast RE-free (a), 1Gd (b) and 1Gd1Nd (c) samples.
Table 3.
Results of cast specimens point composition analysis from Figure 5.
In the as-cast RE-free (Mg–3Zn–0.3Mn) alloy, the microstructure exhibits a typical eutectic morphology, consisting of a dark α-Mg matrix and bright, lath-like lamellar phases (Figure 5a). These bright eutectic phases were identified as Mg7Zn3.
With the addition of Gd (Figure 5b), the amount of the bright eutectic phase increases. The eutectic structure becomes refined, and its volume fraction rises. In some regions, adjacent eutectic portions become interconnected, forming a partial network-like morphology. Most of these bright phases convert to the Mg3Gd2Zn3 (W) phase, while the eutectic morphology is largely retained.
With the further addition of Nd (Figure 5c), both Gd and Nd co-enrich in the bright network phase, combining with Zn to form the Mg3RE2Zn3 (RE = Gd + Nd) phase. At this stage, the eutectic network becomes more continuous and its volume fraction further increases. The network is mainly distributed along triangular grain boundaries and intergranular boundaries.
In Figure 5, point A corresponds to the α-Mg matrix. The composition of points C was Mg 70.88 at.%, Zn 23.86 at.%, Mn 0.26 at.%, Gd 5.00 at.%. And the measured compositions of Point D were Mg 74.96 at.%, Zn 16.97 at.%, Gd 3.16 at.%, Nd 4.91 at.%). At both point C and D, the Mg content was still high, and the Zn/RE atomic ratio was larger than that expected for the W-phase alone. Therefore, it is likely that the second phase in these samples is not a single phase but a eutectic mixture of (Mg7Zn3 + W-phase). Mn was almost uniformly distributed in the matrix, and no Mn-rich secondary phases were detected.
After heat treatment (Figure 4b,d,f), the Mg7Zn3 phase in the RE-free alloy nearly disappeared, with Zn dissolving into the α-Mg matrix (Figure 4b). In the Gd (Figure 4d) and Gd-Nd-containing alloys (Figure 4f), the Mg3RE2Zn3 phase also partially redissolved. The lamellar eutectic structure that initially formed a network gradually dissolved; its edges and corners became rounded, and it transformed into fine particles.
3.2. Hardness
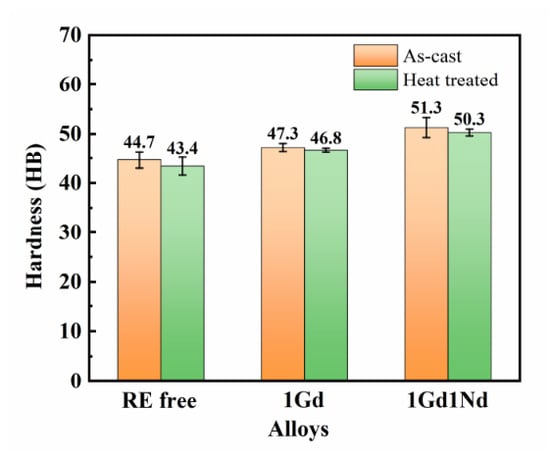
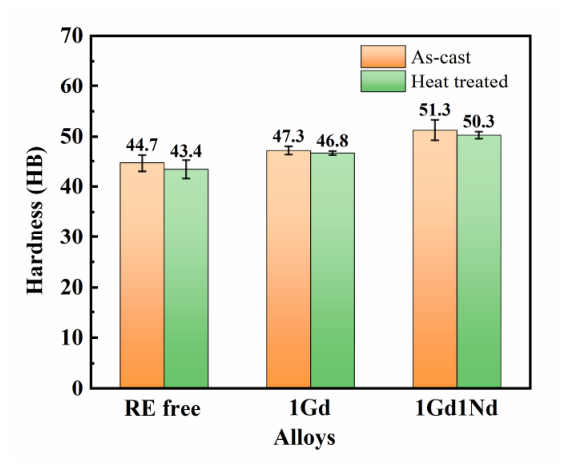
Figure 6 shows the Brinell hardness of the as-cast and heat-treated RE-free, 1Gd, and 1Gd1Nd samples. In the as-cast condition, the hardness values were 44.7 ± 1.7 HB for the RE-free alloy, 47.3 ± 0.8 HB for the 1Gd alloy, and 51.3 ± 2 HB for the 1Gd1Nd alloy. After heat treatment, the hardness values were 43.4 ± 1.8 HB, 46.8 ± 0.4 HB, and 50.3 ± 0.7 HB, respectively.
Figure 6.
Brinell hardness of as-cast and heat-treated RE-free, 1Gd and 1Gd1Nd samples.
In both conditions, the addition of Gd alone increased the hardness, and the co-addition of Gd and Nd further increased it. For each composition, the heat-treated samples showed slightly lower hardness than the as-cast ones, but the decrease was small.
3.3. Friction and Wear Properties
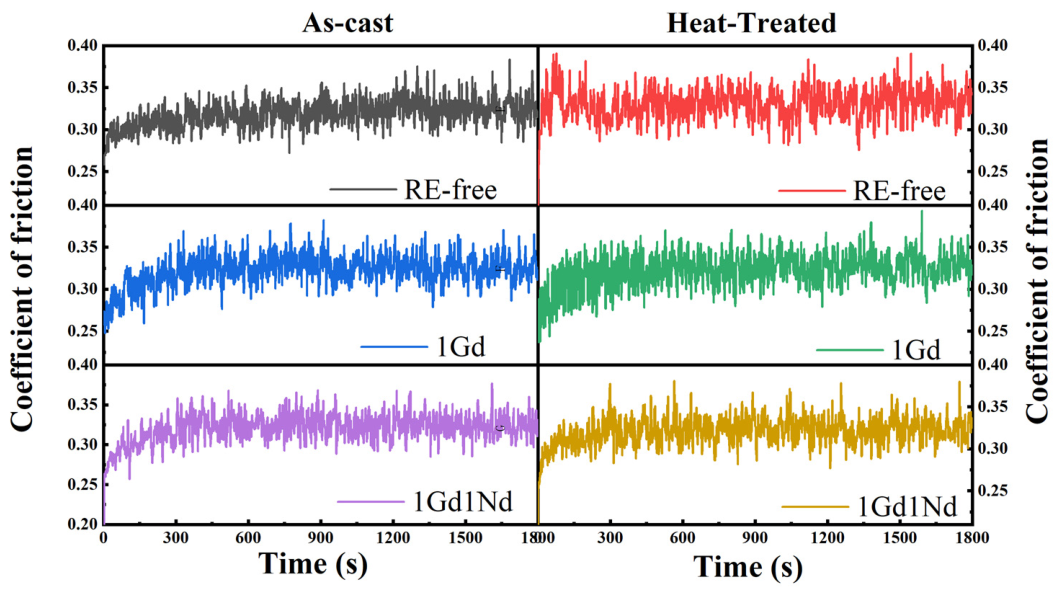
Figure 7 shows the friction coefficient vs. time curves and Table 4 lists the average coefficient of friction (COF) and wear rate of three alloys in the as-cast and heat-treated states under a load of 50 N. The variation range of the friction coefficient is relatively small (0.319–0.330), and the data of each group overlap within the error range, indicating that the friction coefficient is less sensitive to the changes in alloy composition and microstructure, and is not suitable as the main indicator for evaluating wear resistance.
Figure 7.
Friction coefficient vs. time curves of as-cast and heat-treated RE-free, 1Gd and 1Gd1Nd alloy (N = 50 N).
Table 4.
Average friction coefficient and wear rate of as-cast and heat-treated RE-free, 1Gd and 1Gd1Nd alloy.
In contrast, the wear rate shows significant and regular changes, reflecting the essential influence of the microstructure on the wear-resistant performance. In the as-cast state, the wear rate decreases successively with the addition of rare earths: RE-free (0.88) > 1Gd (0.73) > 1Gd1Nd (0.61). This trend is basically consistent with the change in hardness (44.7 → 47.3 → 51.3 HB), indicating that under as-cast conditions, the addition of rare earths improves the hardness through grain refinement strengthening and solid-solution strengthening, thereby improving the wear resistance. The combined addition of 1Gd1Nd has the best effect, and the wear rate is reduced by 30.5% compared with that without rare earths.
Combined with Figure 6 and Table 4, after heat treatment, the hardness of each alloy decreased slightly (by 1–3%), but the wear rate further decreased. For example, in the RE-free alloy, hardness dropped from 44.7 HB to 43.4 HB (↓2.9%), while the wear rate dropped from 0.88 to 0.67 (↓23.9%). In the 1Gd1Nd alloy, hardness decreased from 51.3 HB to 50.3 HB (↓1.9%), and the wear rate decreased from 0.61 to 0.60 (↓3.1%). These results suggest that the improvement in wear resistance after solution treatment is not due to increased hardness but rather to microstructural optimization.
During the wear process, the second phase is prone to brittle fracture and spalling, forming wear debris and aggravating wear. However, the discretely distributed second phase after solution treatment effectively avoids this problem. A matrix with a more uniform composition helps to form a continuous and dense oxide film (a composite oxide containing Gd/Nd) on the worn surface. This film can act as a solid lubricant and protect the matrix, reducing the wear rate. The discrete second-phase particles can serve as a “load-bearing phase” to evenly share the contact stress, reducing local plastic deformation and crack initiation. It is worth noting that the 1Gd1Nd alloy still maintains the lowest wear rate (0.60) after solution treatment, which benefits from the combined addition benefit of Gd and Nd: Gd promotes fine-grain strengthening, while Nd stabilizes the W-phase structure, enabling the second phase to be more uniformly distributed and maintain a small size during the solution process. The heat-treated 1Gd1Nd alloy has the best comprehensive wear performance, which is 32.6% lower than that of the as-cast RE-free alloy.
In this situation, the wear behavior was controlled by hardness and microstructure. Although the solution treatment caused a slight decrease in hardness, its beneficial effect on the morphology and distribution of the secondary phase dominated the improvement in wear performance. The heat-treated 1Gd1Nd alloy achieved the best wear resistance, which supports its potential application as a biomedical implant material.
3.4. Tensile Properties
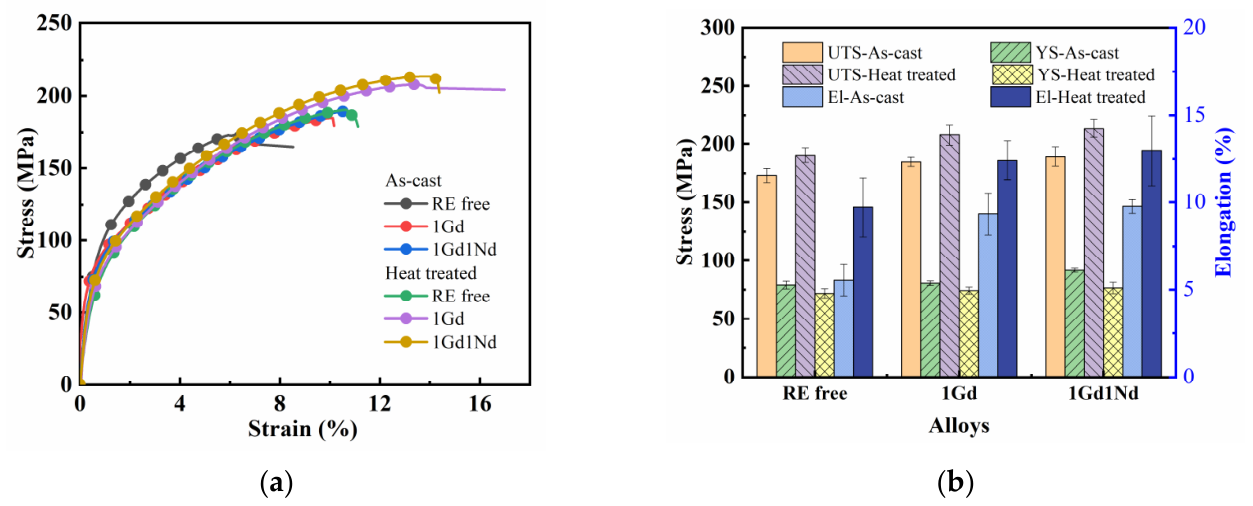
Figure 8 presents the engineering stress-strain curves and room-temperature tensile properties of the three alloys (RE-free, 1Gd, and 1Gd1Nd) in both as-cast and heat-treated conditions. Under both processing conditions, the shapes of the stress-strain curves (Figure 8a) were highly similar across the three compositions, with some curves almost overlapping. All curves exhibited typical brittle cleavage fracture characteristics. The elastic deformation stage was mainly in the range of 0–75 MPa. However, the elongation during the plastic deformation stage and the maximum fracture strength varied considerably. This indicates that the fracture behavior was governed by both strength and ductility, and that the effects of rare-earth addition and heat treatment on these two properties were not fully aligned.
Figure 8.
Engineering stress-strain curves (a), tensile properties (b) of tensile strength, yield strength and elongation of as-cast and heat-treated RE-free, 1Gd and 1Gd1Nd alloys.
With the successive addition of Gd and Nd elements, the strength and elongation of the as-cast alloy both show a certain degree of improvement. The as-cast ZM30 alloy without rare earth elements has the lowest strength, with its yield strength and tensile strength being 78.97 Mpa and 173.27 Mpa respectively. When Gd and Nd are added in combination, the strength of the as-cast alloy is significantly improved. The yield strength and tensile strength reach 91.55 Mpa and 189.38 Mpa respectively, and the elongation after fracture increases from 5.54% to 9.76%. When only Gd is added, the alloy performance is relatively close to that of the sample with combined addition. Its yield strength and tensile strength are 80.62 Mpa and 184.95 Mpa respectively, and the elongation is 9.34%. In the as-cast state, the improvement of strength by rare earth addition is mainly attributed to grain refinement strengthening (Gd) and solid solution strengthening (Gd/Nd), while the increase in elongation is related to the improvement of the second-phase morphology (partial transformation of Mg7Zn3 to W phase), which reduces the stress concentration sources.
Compared with the as-cast samples, the heat-treated alloys showed improved tensile strength and elongation, but the yield strength exhibited different trends. The stress-strain curve of the heat-treated RE-free alloy almost overlapped with that of the as-cast 1Gd1Nd alloy. Its tensile strength was 190.41 Mpa, yield strength 74.08 Mpa, and elongation 9.71%. Notably, after heat treatment, the yield strength of the RE-free alloy decreased slightly from its as-cast value (78.97 Mpa), and those of the 1Gd and 1Gd1Nd alloys also decreased from 80.62 and 91.55 Mpa to 74.08 and 76.49 Mpa, respectively. This may be due to slight grain growth and partial dissolution of secondary phases during near-solidus heat treatment, which weakened grain boundary and dispersion strengthening. However, compositional homogenization and optimization of second-phase morphology (from continuous network to discrete distribution) improved tensile strength and elongation.
As shown in Figure 8b, the heat-treated 1Gd1Nd alloy exhibited the highest tensile and yield strengths, reaching 213.71 and 76.49 Mpa, respectively, with an elongation of 12.96%. The heat-treated 1Gd alloy showed slightly lower values: tensile strength 207.88 Mpa, yield strength 74.08 Mpa, and elongation 12.41%. Overall, the mechanical property trends after heat treatment were consistent with those observed in the as-cast state.
An interesting observation is that the tensile curve of the heat-treated RE-free alloy almost coincides with that of the as-cast 1Gd1Nd alloy. Their tensile strengths (190.41 MPa vs. 189.38 Mpa) and elongations (9.71% vs. 9.76%) are very close. This similarity also appears in the corrosion and wear data; for example, the wear rate of the heat-treated RE-free alloy is comparable to that of the as-cast 1Gd1Nd alloy. These results suggest that near-solidus heat treatment can, to some extent, “simulate” the microstructural benefits of rare-earth addition. By eliminating segregation and improving second-phase morphology, the treatment raises the performance of the RE-free alloy to a level near that of the as-cast RE-containing alloy.
However, heat treatment and rare-earth addition are not fully equivalent. The heat-treated 1Gd1Nd alloy still shows the best performance, confirming that the combined addition benefit of Gd and Nd (grain refinement + W-phase stability) cannot be completely replaced by heat treatment.
In summary, the combination of Gd + Nd addition and near-solidus heat treatment has a co-addition strengthening effect. Rare-earth addition establishes the basis for fine-grain and second-phase strengthening, while heat treatment further optimizes the distribution and stability of the second phase. As a result, the heat-treated 1Gd1Nd alloy achieves the best overall mechanical properties, with a tensile strength of 213.71 Mpa and an elongation of 12.96%, both meeting the basic requirements for biomedical implant materials.
3.5. Corrosion Properties
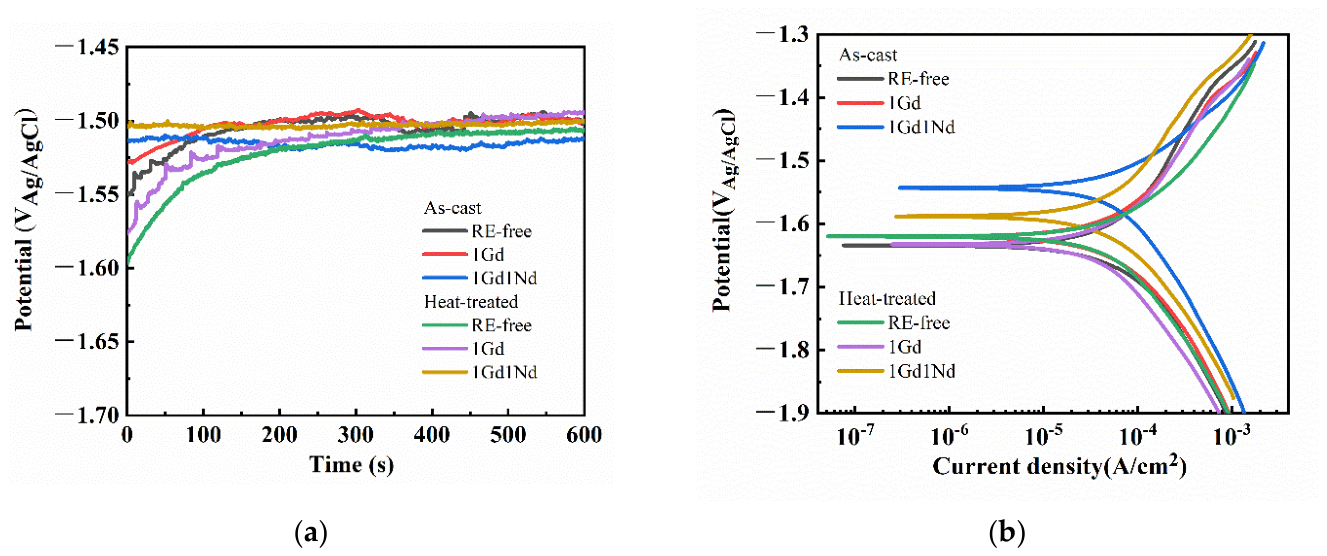
Figure 9 shows the open-circuit potential (OCP) curves and potentiodynamic polarization curves of the RE-free, 1Gd, and 1Gd1Nd samples in the as-cast and heat-treated states.
Figure 9.
The open-circuit potential (OCP) curves (a) and potentiodynamic polarization curves (b) of the RE-free, 1Gd, and 1Gd1Nd samples in the as-cast and heat-treated states.
From Figure 9a, the OCP of all samples gradually stabilized after about 150 s. The stable potential ranged from −1.52 V to −1.50 V. In the initial stage, the starting potentials were: −1.60 V for the heat-treated RE-free sample, −1.58 V for the heat-treated 1Gd sample, −1.55 V for the as-cast RE-free sample, and −1.53 V for the as-cast 1Gd sample. In contrast, the 1Gd1Nd samples in both conditions showed very small potential fluctuations. The as-cast 1Gd1Nd potential fluctuated around −1.51 V, and the heat-treated 1Gd1Nd fluctuated around −1.50 V.
Throughout the test, the1Gd1Nd samples (both as-cast and heat-treated) exhibited the most stable OCP. This indicates that a more stable and compact oxide film formed on their surfaces. This behavior is attributed to the combined addition benefit of Gd and Nd. Gd promotes grain refinement and rapid film formation, while Nd improves the structural stability of the oxide film. Heat treatment also aids compositional homogenization, further enhancing the protectiveness of the film.
From the potentiodynamic polarization curves in Figure 9b and the Tafel extrapolation data in Table 5, the following trends were observed. With the addition of rare earth elements, the self-corrosion potential (Ecorr) of the as-cast alloys shifted positively: −1.63 V (RE-free) < −1.62 V (1Gd) < −1.54 V (1Gd1Nd). The corrosion current density (icorr) decreased in the same order: 1.1 × 10⁻⁴ (RE-free) > 8.86 × 10⁻⁵ (1Gd) > 8.59 × 10⁻⁵ mA/cm2 (1Gd1Nd). The corrosion rate also followed this trend: 3.61 mm/y (RE-free) > 2.91 mm/y (1Gd) > 2.80 mm/y (1Gd1Nd). These results indicate that, in the as-cast state, rare earth addition effectively improved the thermodynamic stability of the alloy and suppressed the cathodic reaction. This is attributed to grain refinement and the formation of a more stable W-phase (Mg3RE2Zn3).
Table 5.
Polarization curve parameters obtained by Tafel extrapolation method.
After heat treatment, the self-corrosion potential (Ecorr) of the three samples shifted further in the positive direction: −1.63 V (RE-free) < −1.62 V (1Gd) < −1.59 V (1Gd1Nd). The corrosion current density (icorr) decreased in the same order: 8.52 × 10⁻⁵ (RE-free) > 8.32 × 10⁻⁶ (1Gd) > 8.16 × 10⁻⁶ mA/cm2 (1Gd1Nd). The corrosion rates also followed this trend: 2.78 mm/y (RE-free) > 2.72 mm/y (1Gd) > 2.68 mm/y (1Gd1Nd).
Compared with the as-cast state, all heat-treated samples showed improved corrosion resistance. Notably, the improvement was most significant for the RE-free alloy: its corrosion rate decreased from 3.61 to 2.78 mm/y (a reduction of about 23.0%). In contrast, the 1Gd1Nd alloy showed only a small decrease, from 2.80 to 2.68 mm/y (a reduction of about 4.3%). These results suggest that heat treatment improves corrosion resistance mainly by eliminating compositional segregation and promoting the dissolution and transformation of the continuous network-like secondary phase (Mg7Zn3 → W-phase).
For the 1Gd1Nd alloy, which already has an optimized microstructure through rare-earth addition, the additional benefit of heat treatment is limited. Nevertheless, the heat-treated 1Gd1Nd sample still exhibited the lowest corrosion current density and corrosion rate, confirming that the combined addition benefit of Gd and Nd remains effective after heat treatment.
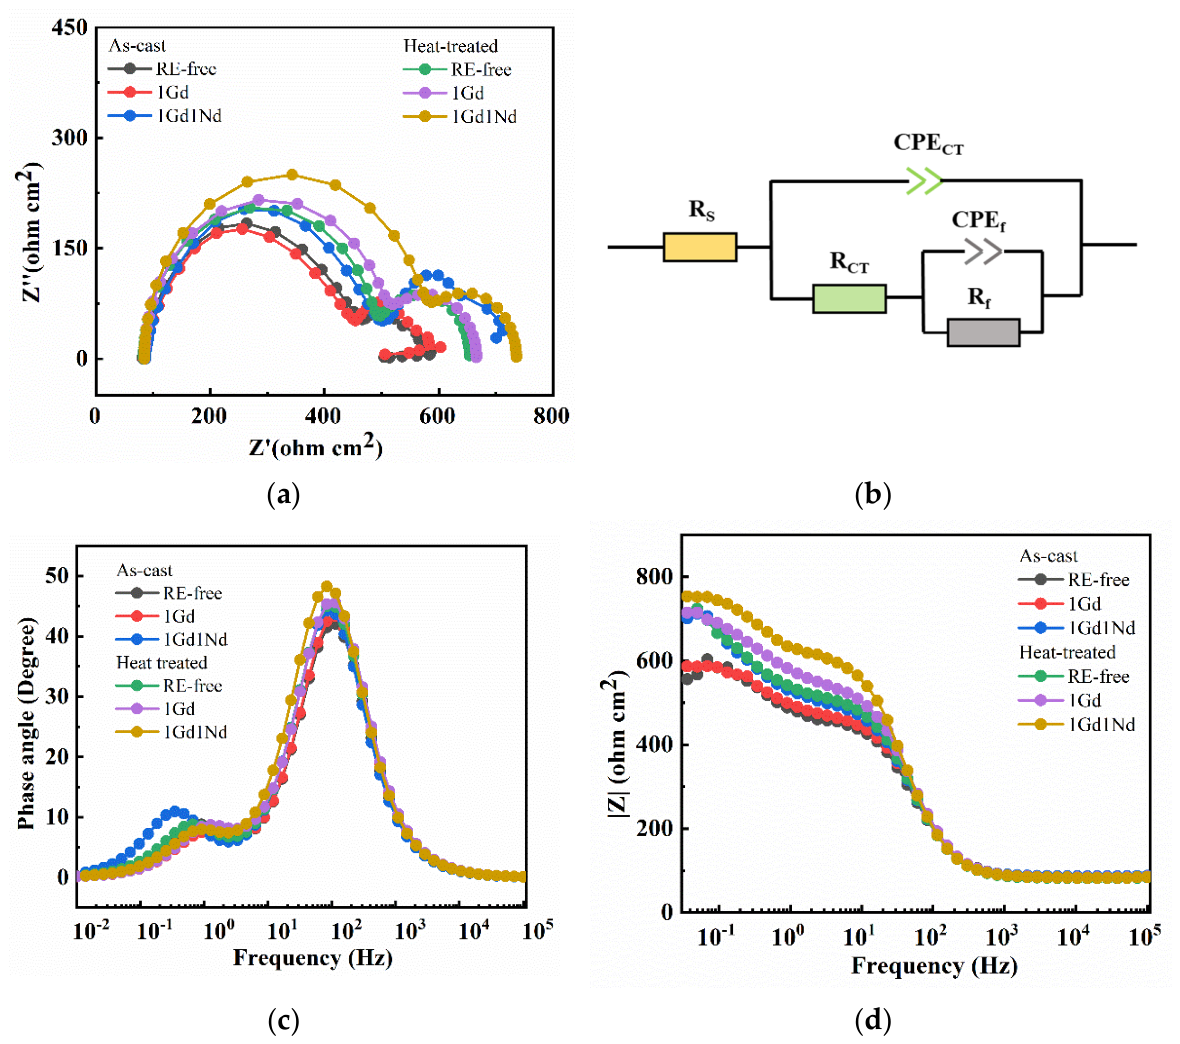
Figure 10 presents the electrochemical impedance spectroscopy (EIS) results for the as-cast and heat-treated RE-free, 1Gd, and 1Gd1Nd samples in Hank’s solution. Specifically, Figure 10a shows the Nyquist plots, Figure 10b the equivalent circuit used for fitting, Figure 10c the Bode plots of phase angle vs. frequency, and Figure 10d the Bode plots of impedance modulus vs. frequency. The fitted parameters obtained with the equivalent circuit (including ) are summarized in Table 6.
Figure 10.
As-cast and heat-treated RE-free, 1Gd, and 1Gd1Nd specimens in Hank’s solution electrochemical performance test: (a) Nyquist diagram; (b) Fitting circuit diagram; (c) Bode diagram of phase angle varying with frequency; (d) Bode diagram of impedance varying with frequency.
Table 6.
Electrochemical impedance spectroscopy fitting data of as-cast and heat-treated RE-free, 1Gd and 1Gd1Nd specimens.
From the Nyquist plots in Figure 10a, the as-cast RE-free and 1Gd alloys showed relatively similar reactance arcs. In contrast, the reactance arc of the as-cast 1Gd1Nd sample was clearly larger. This indicates higher charge transfer resistance and better corrosion resistance. After heat treatment, the reactance arcs of all three samples became larger than those of their as-cast counterparts. The trend remained similar: the 1Gd1Nd sample had the largest arc, while the other two alloys showed arcs close to each other. These results indicate that both heat treatment and rare-earth addition effectively increase the charge transfer resistance on the alloy surface.
From the phase angle Bode plots in Figure 10d, each sample curve shows two distinct phase angle peaks. This indicates that the corrosion process in Hank‘s solution involves two time constants, corresponding to the corrosion product film (high-frequency region) and charge transfer (low-frequency region). Notably, the first peak (high frequency) is highest for the as-cast 1Gd1Nd sample, while the second peak (low frequency) is highest for the heat-treated 1Gd1Nd sample. This suggests that the as-cast 1Gd1Nd alloy has better initial film-forming ability, whereas after heat treatment, the charge transfer process becomes more dominant.
From the impedance modulus Bode plots in Figure 10d, the low-frequency (0.01 Hz) impedance modulus |Z| is an important indicator of corrosion resistance. A higher |Z| value means a more protective corrosion product film on the substrate. In the figure, all heat-treated samples showed higher |Z| values than their as-cast counterparts. Among them, the heat-treated 1Gd1Nd alloy exhibited the highest |Z| value, further confirming that the combination of dual rare-earth elements and heat treatment significantly improves the corrosion resistance of magnesium alloys.
Table 6 lists the fitted EIS parameters. In the equivalent circuit, is the solution resistance. and represent the constant phase element and resistance of the corrosion product film, respectively. and correspond to the constant phase element and charge transfer resistance of the electrochemical reaction. Generally, a larger value indicates higher resistance to electrochemical reactions on the alloy surface, and thus better corrosion resistance. The value reflects the protective ability of the corrosion product film on the underlying metal.
In the as-cast condition, both and increased with rare-earth addition. For the RE-free alloy, was 352.80 Ω·cm2 and was 113.10 Ω·cm2. After adding 1Gd, rose to 367.80 Ω·cm2 and to 139.30 Ω·cm2. With the combined addition of 1Gd and 1Nd, further increased to 409.40 Ω·cm2 and to 219.40 Ω·cm2.
This trend is fully consistent with the changes in corrosion current density and corrosion rate obtained from the potentiodynamic polarization curves. It indicates that rare-earth addition effectively increases the charge transfer resistance on the alloy surface and improves the protectiveness of the corrosion product film. Notably, the value of the 1Gd1Nd alloy (219.40 Ω·cm2) is much higher than those of the RE-free and 1Gd alloys. This suggests that the combined addition of Gd and Nd significantly enhances the compactness and stability of the corrosion product film.
After heat treatment, both and increased for all alloys compared to their as-cast values, but the degree of increase varied with composition. For the RE-free alloy, increased from 352.80 to 432.90 Ω·cm2 (+22.7%), and from 113.10 to 147.60 Ω·cm2 (+30.5%). For the 1Gd alloy, rose from 367.80 to 500.30 Ω·cm2 (+36.0%), and from 139.30 to 150.60 Ω·cm2 (+8.1%). For the 1Gd1Nd alloy, increased only slightly from 409.40 to 412.30 Ω·cm2 (+0.7%), while decreased from 219.40 to 158.30 Ω·cm2 (still a relatively high value).
These results indicate that heat treatment more effectively enhanced the charge transfer resistance of the RE-free and 1Gd alloys. For the 1Gd1Nd alloy, which already had a high in the as-cast state, the additional benefit of heat treatment was limited. This trend agrees well with the corrosion rate changes from the polarization curves (a 23.0% reduction for the RE-free alloy vs. only 4.3% for the 1Gd1Nd alloy). It further confirms that heat treatment improves corrosion resistance mainly by eliminating compositional segregation and optimizing second-phase morphology. For alloys whose microstructure has already been optimized by rare-earth addition, the marginal benefit of heat treatment is smaller.
A comprehensive comparison shows that the heat-treated 1Gd alloy had the highest value (500.30 Ω·cm2), while the as-cast 1Gd1Nd alloy had the highest value (219.40 Ω·cm2). The heat-treated 1Gd1Nd alloy exhibited relatively high values of both (412.30 Ω·cm2) and (158.30 Ω·cm2). Together with its lowest corrosion current density (8.16 × 10⁻⁶ mA/cm2) and corrosion rate (2.68 mm/y), the heat-treated 1Gd1Nd alloy showed the best overall corrosion resistance. This is attributed to the combined addition benefit of Gd and Nd, which optimizes the fine-grained structure, stabilizes the W-phase, and improves the density of the corrosion product film.
The EIS results are in good agreement with the potentiodynamic polarization data, mutually confirming the beneficial synergy of rare earth addition and heat treatment on corrosion resistance.
4. Discussion
This study systematically compared the microstructure, mechanical properties, corrosion behavior and friction-milling performance of three Mg-Zn-Mn-based alloys (RE-free, 1Gd, and 1Gd1Nd) under as-cast and heat-treated conditions. The aim was to clarify the co-addition regulation mechanism of rare earth microalloying and heat treatment processes on the comprehensive properties of the alloys. The following discussion will focus on three aspects: “rare earth addition effect”, “heat treatment effect” and “Gd-Nd synergy mechanism”.
4.1. Rare Earth Addition on Microstructure and Properties
In the as-cast condition, the addition of Gd and Nd significantly changed the microstructure of the alloys. The RE-free alloy had relatively coarse grains (~28 μm), and the secondary phase was distributed along the grain boundaries as a continuous network of Mg7Zn3. After adding 1% Gd, the grains refined to about 11 μm, and the secondary phase gradually transformed into the W-phase (Mg3RE2Zn3). With the combined addition of Gd and Nd, the grains further refined to roughly 8 μm, and the W-phase became more uniformly and dispersedly distributed.
This microstructural evolution can be explained by two mechanisms [23,33,34,35,36]. First, the larger atomic radii of Gd and Nd cause a solute drag effect at the solid-liquid interface, which inhibits grain growth. Second, the W-phase acts as a heterogeneous nucleation site, promoting grain refinement during dynamic recrystallization.
The microstructural optimization caused by rare earth addition was directly reflected in the mechanical and corrosion properties. In the as-cast state, hardness increased successively (44.7 HB → 47.3 HB → 51.3 HB), and tensile strength and elongation also improved. These trends agree with the classic concepts of grain refinement strengthening and dispersion strengthening.
Regarding corrosion performance, the 1Gd1Nd alloy exhibited the most positive corrosion potential (−1.54 V), the lowest corrosion current density (8.59 × 10⁻⁵ mA/cm2), and the lowest corrosion rate (2.80 mm/y). Its charge transfer resistance () and film resistance () were significantly higher than those of the RE-free and 1Gd alloys (Table 6). Notably, the value of the 1Gd1Nd alloy (219.4 Ω·cm2) was much higher than those of the other as-cast alloys. This indicates that the corrosion product film formed through Gd-Nd synergy was denser and more stable.
This behavior is related to the smaller galvanic potential difference between the W-phase and the α-Mg matrix after phase transformation. In addition, rare-earth ions (Gd3+, Nd3+) incorporated into the corrosion product film as Gd(OH)3 and Nd(OH)3/Nd2O3, which reduced the dissolution rate of the film [36].
The wear performance also benefited from rare-earth addition. In the as-cast state, the wear rate decreased in the order: RE-free (0.883) > 1Gd (0.729) > 1Gd1Nd (0.614) (×10−3 mm3/(N·m)). The friction coefficient showed little change, but the significant reduction in wear rate was directly related to the increase in hardness and the improved morphology of the secondary phase. The fine W-phase particles acted as load-bearing constituents during sliding, reducing plastic extrusion of the matrix and abrasive wear.
4.2. Heat Treatment on Microstructure and Properties
The heat treatment temperatures used in this study were selected based on the melting temperatures of the secondary phases in the RE-free alloy, as determined by DSC. Compared with the as-cast state, all heat-treated samples showed the following common changes. The grain size increased slightly; for example, the RE-free alloy showed a small increase in grain size (hardness decreased by 1–3%). The secondary phase morphology changed from a continuous network or coarse particles to a more discrete and uniform distribution, and part of the Mg7Zn3 phase dissolved. Compositional segregation was reduced, and the homogeneity of the matrix improved.
These microstructural changes led to an interesting and scientifically important outcome: after heat treatment, hardness decreased slightly, but corrosion resistance and wear resistance improved significantly. Taking the RE-free alloy as an example, hardness dropped from 44.7 HB to 43.4 HB (–2.9%), while the corrosion rate decreased from 3.61 to 2.78 mm/y (–23.0%) and the wear rate from 0.883 to 0.672 (–23.9%). This clearly shows that the improvement in performance after heat treatment was not due to increased hardness, but rather to changes in the morphology and distribution of the secondary phases.
First, after solution treatment, the Mg7Zn3 phase disappears. The continuous network-like secondary phase also disappears. This reduces the number of micro-galvanic pairs that are prone to corrosion and also prevents the detachment of brittle phases during wear. Second, the redistribution of Zn and rare-earth elements in the matrix, together with compositional homogenization, lowers the local corrosion sensitivity. It also promotes the formation of a more continuous and denser oxide film, as supported by the increase in |Z| and the changes in values. Finally, heat treatment does not eliminate the W-phase. This phase remains and possesses superior chemical inertness and mechanical stability, thereby improving corrosion resistance, wear resistance, and mechanical properties.
For the alloys already containing rare earth elements, especially 1Gd1Nd, the additional benefit of heat treatment was relatively small. The corrosion rate decreased only from 2.80 to 2.68 mm/y (–4.3%), and even dropped slightly (from 219.4 to 158.3 Ω·cm2). However, remained stable, and the |Z| value reached the highest among all samples, indicating that heat treatment still improved the charge transfer process. These results suggest that when an alloy already has an optimized microstructure through rare earth microalloying, the further improvement from heat treatment is limited. Nevertheless, the combination of both still achieved the best overall performance.
4.3. Combined Addition Benefits of Gd and Nd
One of the key findings of this study is that Gd and Nd have a clear co-addition strengthening effect when added together. Compared with the sole addition of Gd, the 1Gd1Nd alloy showed finer grains, higher hardness, better corrosion resistance, and a lower wear rate in both the as-cast and heat-treated states.
This co-addition arises from the complementary roles of the two rare earth elements. Gd has a higher growth restriction factor (GRF) and stronger grain-refining ability. Moreover, Gd oxide/hydroxide has very low solubility, which greatly enhances the stability of the corrosion product film [36]. In contrast, Nd has a stronger affinity for Zn and forms a more stable W-phase (Mg3Nd2Zn3 or a mixed-RE W-phase) [37]. This W-phase is more resistant to dissolution during heat treatment and has a smaller potential difference with the α-Mg matrix.
The combined addition of Gd and Nd not only provides the benefits of both grain refinement and solid solution strengthening but also improves the type and distribution of the secondary phases [31]. As a result, the corrosion current is more evenly spread, and localized pitting is less likely to occur.
4.4. Heat Treatment as a Partial Substitute for Rare-Earth Addition
Another notable observation is that the tensile curve, wear rate, and corrosion rate of the heat-treated RE-free alloy were very close to those of the as-cast 1Gd1Nd alloy. For example, the tensile curves almost overlap (Figure 9), the wear rates were 0.672 vs. 0.614, and the corrosion rates were 2.78 vs. 2.80 mm/y. This suggests that near-solidus heat treatment can, to some extent, “simulate” the microstructural benefits of rare earth addition. By eliminating segregation and adjusting second-phase morphology, heat treatment improves the performance of the base alloy to a level similar to that achieved by rare-earth microalloying.
However, heat treatment cannot completely replace rare-earth addition. The unique electronic structure and chemical activity of rare-earth elements provide additional benefits, such as the formation of RE hydroxide/oxide composite films, which simple heat treatment cannot achieve. The combination of heat treatment and Gd + Nd addition gave the best overall performance in this study.
4.5. Limitations and Future Perspectives
Several limitations of the present study should be acknowledged. First, the investigated alloys were examined only in the as-cast and heat-treated states. Their mechanical properties and corrosion resistance, although systematically improved by rare-earth addition and heat treatment, are still insufficient for direct use as load-bearing biodegradable implants (e.g., bone plates or screws). Second, only one set of heat treatment parameters was used; the full process window remains to be optimized. Third, long-term degradation behavior (more than 30 days) and intracorporeal implantation experiment were not assessed.
It should be emphasized that the present work is part of a broader research effort. The same alloy system (Mg–3Zn–0.3Mn with Gd/Nd additions) has been further processed by hot extrusion following the same heat treatment. In our companion study (currently under review), the extruded alloys exhibit significantly improved mechanical properties and corrosion resistance, making them more suitable for biodegradable implant applications. Therefore, the current study provides a microstructural and property baseline for the precursor materials (as-cast and heat-treated states) before severe plastic deformation. The knowledge gained here—particularly the combined addition benefit of Gd and Nd, the role of the W-phase, and the influence of heat treatment on second-phase morphology—directly supports the optimization of the extrusion process and helps to understand the property evolution from the cast to the wrought state.
In future work, the following aspects should be addressed: (1) systematic characterization of the extruded alloys, including long-term immersion tests, wear testing under physiological loads, and cytotoxicity evaluation; (2) optimization of the heat-treatment parameters (temperature and time) to further enhance the precursor microstructure; (3) exploration of semi-solid forming or additive manufacturing for this alloy system. Overall, the present study lays a foundation for developing high-performance biodegradable magnesium alloys through a combined strategy of rare-earth microalloying, optimized heat treatment, and subsequent hot extrusion.
5. Conclusions
Three Mg–3Zn–0.3Mn alloys (RE-free, 1Gd, and 1Gd1Nd) were prepared by casting. A part of each alloy was then subjected to near-solidus heat treatment at 460 °C for 12 h. The microstructure, mechanical properties, corrosion behavior in Hank’s solution, and dry sliding wear resistance were systematically characterized. The properties of the as-cast and heat-treated samples were systematically compared to evaluate the individual and combined effects of rare-earth addition and heat treatment.
- (1)
- Rare earth addition, especially the combined addition of Gd and Nd, refined the grains, transformed the secondary phase from Mg7Zn3 to the W-phase (Mg3RE2Zn3), and simultaneously improved the hardness, tensile strength, corrosion resistance and wear resistance of the as-cast alloys. The 1Gd1Nd alloy showed the best overall performance.
- (2)
- Near-solidus heat treatment slightly decreased hardness (1–3%) but significantly enhanced corrosion resistance (e.g., corrosion rate of RE-free alloy decreased by 23.0%) and wear resistance. The heat-treated RE-free alloy exhibited properties close to those of the as-cast 1Gd1Nd alloy, indicating that heat treatment can partially “simulate” the microstructural benefits of rare earth addition by eliminating segregation and optimizing second-phase morphology.
- (3)
- Gd and Nd exhibited a clear combined addition benefit: Gd promoted grain refinement and stable oxide film formation, while Nd stabilized the W-phase and reduced the galvanic potential difference with the α-Mg matrix. The combination of Gd/Nd co-addition and near-solidus heat treatment gave the best comprehensive properties, providing a foundation for further processing (e.g., hot extrusion) to achieve performance suitable for biodegradable implant applications.
Author Contributions
Conceptualization, X.L., M.Y. and Z.C.; Methodology, X.Y. and S.Q.; Software, X.Y. and S.Q.; Validation, X.L., M.Y. and Z.C.; Formal Analysis, X.L.; Investigation, X.Y. and S.Q.; Resources, M.Y. and Z.C.; Data Curation, X.Y. and S.Q.; Writing—Original Draft Preparation, X.Y. and M.Y.; Writing—Review & Editing, M.Y.; Supervision, Z.C.; Project Administration, M.Y.; Funding Acquisition, M.Y. and Z.C. All authors have read and agreed to the published version of the manuscript.
Funding
This research was funded by the Natural Science Foundation of Jilin Province, China (grant number YDZJ202601ZYTS113), and the Science and Technology Research Project of the Education Department of Jilin Province, China (grant number JJKH20250810KJ).
Data Availability Statement
The original contributions presented in this study are included in the article. Further inquiries can be directed to the corresponding author.
Acknowledgments
The authors gratefully acknowledge the technical support extended by Fengyun Yu from the School of Materials Science and Engineering, Dalian University of Technology.
Conflicts of Interest
The authors declare no conflicts of interest.
References
- Tsakiris, V.; Tardei, C.; Clicinschi, F. Biodegradable Mg Alloys for Orthopedic Implants—A Review. J. Magnes. Alloys 2021, 9, 1884–1905. [Google Scholar] [CrossRef] [Scilit]
- Zhang, Z.; Yang, Y.; Li, J.; Zeng, R.; Guan, S. Advances in Coatings on Magnesium Alloys for Cardiovascular Stents—A Review. Bioact. Mater. 2021, 6, 4729–4757. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Zhi, P.; Liu, L.; Chang, J.; Liu, C.; Zhang, Q.; Zhou, J.; Liu, Z.; Fan, Y. Advances in the Study of Magnesium Alloys and Their Use in Bone Implant Material. Metals 2022, 12, 1500. [Google Scholar] [CrossRef] [Scilit]
- Púa, L.; Montenegro, J.; Reyes, A.; Rodríguez, H.; Méndez, V. Biomaterials for Orthopedic Applications and Techniques to Improve Corrosion Resistance and Mechanical Properties for Magnesium Alloy: A Review. J. Mater. Sci. 2023, 58, 3879–3908. [Google Scholar] [CrossRef] [Scilit]
- Yang, M.; Chen, C.; Wang, D.; Shao, Y.; Zhou, W.; Shuai, C.; Yang, Y.; Ning, X. Biomedical Rare-Earth Magnesium Alloy: Current Status and Future Prospects. J. Magnes. Alloys 2024, 12, 1260–1282. [Google Scholar] [CrossRef] [Scilit]
- He, M.; Chen, L.; Yin, M.; Xu, S.; Liang, Z. Review on Magnesium and Magnesium-Based Alloys as Biomaterials for Bone Immobilization. J. Mater. Res. Technol. 2023, 23, 4396–4419. [Google Scholar] [CrossRef] [Scilit]
- Xu, Z.; Zhang, J.; He, Y.; Yang, Q.; Liu, S.; Zhao, T.; Dong, H.; Wu, R.; Zhang, X.; Qiu, X. Revealing Anti-Corrosion Mechanism of Low-Alloyed Mg-Gd-Zn-Zr Alloy with Ultra-Low Corrosion Rate. Corros. Sci. 2025, 251, 112931. [Google Scholar] [CrossRef] [Scilit]
- Singh, N.; Batra, U.; Kumar, K.; Ahuja, N.; Mahapatro, A. Progress in Bioactive Surface Coatings on Biodegradable Mg Alloys: A Critical Review towards Clinical Translation. Bioact. Mater. 2023, 19, 717–757. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Wang, S.; Du, C.; Shen, X.; Wu, X.; Ouyang, S.; Tan, J.; She, J.; Tang, A.; Chen, X.; Pan, F. Rational Design, Synthesis and Prospect of Biodegradable Magnesium Alloy Vascular Stents. J. Magnes. Alloys 2023, 11, 3012–3037. [Google Scholar] [CrossRef] [Scilit]
- Mahmud, S.; Rahman, M.; Kamruzzaman, M.; Khatun, H.; Ali, M.; Haque, M. Recent Developments in Hydroxyapatite Coating on Magnesium Alloys for Clinical Applications. Results Eng. 2023, 17, 101002. [Google Scholar] [CrossRef] [Scilit]
- Wu, X.; Zhu, L.; Jing, X.; Sirag, Z.; Niu, E.; Yuan, H.; She, J. Biodegradable Mg-Zn-Mn Alloys for Orbital Bone Fixation: Balancing Corrosion Resistance and Mechanical Integrity. J. Mater. Res. Technol. 2026, 40, 98–113. [Google Scholar] [CrossRef] [Scilit]
- Asadollahi, M.; Gerashi, E.; Alizadeh, R.; Mahmudi, R. Effect of Zn Content and Processing Route on the Microstructure, Mechanical Properties, and Bio- Degradation of Mg-Zn Alloys. J. Mater. Res. Technol. 2022, 21, 4473–4489. [Google Scholar] [CrossRef] [Scilit]
- Zhao, X.; Li, S.; Yan, F.; Zhang, Z.; Wu, Y. Microstructure Evolution and Mechanical Properties of AZ80 Mg Alloy during Annular Channel Angular Extrusion Process and Heat Treatment. Materials 2019, 12, 4223. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Li, C.; Xia, Z.; Qiao, X.; Golovin, I.; Zheng, M. Superior Ductility Mg-Mn Extrusion Alloys at Room Temperature Obtained by Controlling Mn Content. Mater. Sci. Eng. A 2023, 869, 144508. [Google Scholar] [CrossRef] [Scilit]
- Tong, L.; Zheng, M.; Xu, S.; Kamado, S.; Du, Y.; Hu, X.; Wu, K.; Gan, W.; Brokmeier, H.; Wang, G.; et al. Effect of Mn Addition on Microstructure, Texture and Mechanical Properties of Mg-Zn-ca Alloy. Mater. Sci. Eng. A 2011, 528, 3741–3747. [Google Scholar] [CrossRef] [Scilit]
- Deng, H.; Yang, Y.; Li, M.; Xiong, X.; Wei, G.; Xie, W.; Jiang, B.; Peng, X.; Pan, F. Effect of Mn Content on the Microstructure and Mechanical Properties of Mg-6Li-4Zn-xMn Alloys. Prog. Nat. Sci. Mater. Int. 2021, 31, 583–590. [Google Scholar] [CrossRef] [Scilit]
- Xiao, C.; Sun, S.; Meng, D.; Ren, Y.; Zheng, Y.; Su, Y.; Liu, B.; Zhang, H. Effect of Mn on Microstructures and Properties of Backward Extruded Zn-0.5 Mg Alloys. J. Mater. Res. Technol. 2025, 35, 1546–1555. [Google Scholar] [CrossRef] [Scilit]
- Zhang, D.; Qi, F.; Shi, G.; Dai, Q. Effects of Mn Content on Microstructure and Mechanical Properties of Mg-Zn-Mn Wrought Alloys. Rare Met. Mater. Eng. 2010, 39, 2205–2210. [Google Scholar]
- Qi, F.; Zhang, D.; Zhang, X.; Pan, F. Effect of Y Addition on Microstructure and Mechanical Properties of Mg-Zn-Mn Alloy. Trans. Nonferrous Met. Soc. China 2014, 24, 1352–1364. [Google Scholar] [CrossRef] [Scilit]
- Jiang, N.; Chen, L.; Meng, L.; Fang, C.; Hao, H.; Zhang, X. Effect of Neodymium, Gadolinium Addition on Microstructure and Mechanical Properties of AZ80 Magnesium Alloy. J. Rare Earths 2016, 34, 632–637. [Google Scholar] [CrossRef] [Scilit]
- Wang, Y.; Fu, J.; Yang, Y. Effect of Nd Addition on Microstructures and Mechanical Properties of AZ80 Magnesium Alloys. Trans. Nonferrous Met. Soc. China 2012, 22, 1322–1328. [Google Scholar] [CrossRef] [Scilit]
- Hu, S.; Bo, G.; Li, W.; Zhu, S.; Li, C.; Zhang, C.; Jiang, D.; Peng, Z.; Qiu, W.; Chen, H.; et al. First-Principles Insights into the Influence of Y Content on the Corrosion and Stress Corrosion Cracking Resistance of AZ91 Magnesium Alloy. J. Alloys Compd. 2025, 1032, 181115. [Google Scholar] [CrossRef] [Scilit]
- Lin, Y.; Zhang, X.; Le, Q.; Wang, T.; Liao, Q.; Liu, L. Achieving the Improvement of Tensile Properties and Corrosion Resistance of Mg-Gd-Sn-Y-Zn-Mn Alloy by Increasing the Concentration of Solute Elements in Nearly Equal-Amplitude. J. Alloys Compd. 2025, 1010, 178323. [Google Scholar] [CrossRef] [Scilit]
- Zhou, R.; Zhang, C.; Liu, Z.; Zhang, X.; Li, X.; Zheng, K.; Pan, F. Effect of the Mn Content on the Microstructure and Mechanical Properties of Extruded Mg-9Gd-4Y-1Zn-xMn Series Alloys. Mater. Today Commun. 2025, 42, 111429. [Google Scholar] [CrossRef] [Scilit]
- Ma, K.; Wang, J.; Peng, Y.; Dai, C.; Pan, Y.; Wang, Y.; Wang, D.; Wang, J.; Ma, Y.; Pan, F. Achieving High Strength and Rapid Degradation in Mg-Gd-Ni Alloys by Regulating LPSO Phase Morphology Combined with Extrusion. J. Magnes. Alloys 2024, 12, 2312–2326. [Google Scholar] [CrossRef] [Scilit]
- Zhu, Q.; Fang, C.; Li, N.; Meng, L.; Wang, Y.; Wu, Y.; Zhang, X. Effects of Rare-earth Elements Gd and Nd on Microstructure and Mechanical Properties of AZ80 Magnesium Alloy. Rare Met. Mater. Eng. 2013, 42, 771–775. [Google Scholar]
- Zhao, Y.; Li, H.; Jing, C.; Zhao, F.; Zhang, D.; Pan, F. Improving Tensile Properties and Corrosion Resistance of Mg-Zn-ca-Mn Alloy via Gd Addition. Intermetallics 2023, 162, 108000. [Google Scholar] [CrossRef] [Scilit]
- Yang, M.; Zhang, Z.; Liu, Y.; Han, X. Corrosion and mechanical properties of AM50 magnesium alloy after modified by different amounts of rare earth element gadolinium. Open Phys. 2016, 14, 444–451. [Google Scholar] [CrossRef] [Scilit]
- Li, G.; Kwon, H.; Suh, B.; Han, H.; Jeon, H.; Cha, P.; Kim, D.; Seok, H.; Kim, Y. Development of Biodegradable Mg-Zn Alloys by Grain Refinement through Extrusion. JOM 2025, 77, 4384–4392. [Google Scholar] [CrossRef] [Scilit]
- Yuan, Y.; Ma, A.; Gou, X.; Jiang, J.; Arhin, G.; Song, D.; Liu, H. Effect of Heat Treatment and Deformation Temperature on the Mechanical Properties of ECAP Processed ZK60 Magnesium Alloy. Mater. Sci. Eng. A 2016, 677, 125–132. [Google Scholar] [CrossRef] [Scilit]
- Jana, A.; Das, M.; Balla, V. Effect of Heat Treatment on Microstructure, Mechanical, Corrosion and Biocompatibility of Mg-Zn-Zr-Gd-Nd Alloy. J. Alloys Compd. 2020, 821, 153462. [Google Scholar] [CrossRef] [Scilit]
- Zheng, L.; Liang, W.; Zhao, Z.; Li, Y.; Wang, H.; Wang, Y. Effect of Homogenizing Annealing Treatment on Hot-rolled MicroStructure and Mechanical Properties of AZ91 Magnesium Alloy. Rare Met. Mater. Eng. 2016, 45, 1296–1301. [Google Scholar]
- Dong, Q.; Jiang, J.; Zhang, J.; Hu, Z.; Zhang, X. Clarifying Stress Corrosion Cracking Behavior of Biomedical Mg-Gd-Zn-Zr Alloy. J. Magnes. Alloys 2025, 13, 3450–3465. [Google Scholar] [CrossRef] [Scilit]
- Ji, Z.; Qiao, X.; Sun, W.; Yuan, L.; Cong, F.; Wang, G.; Zheng, M. Effect of Bimodal Microstructure on the Tensile Properties and Fracture Toughness of Extruded Mg-9Gd-4Y-0.5Zr Alloy. Mater. Sci. Eng. A 2023, 885, 145587. [Google Scholar] [CrossRef] [Scilit]
- Zheng, Z.; Dong, Z.; Jiang, B.; Cheng, Y.; Bai, S.; Zhang, A.; Pan, F. Effect of Er Content on Mechanical Properties and Microstructural Evolution of Highly-Alloyed Mg-10Gd-5Y Alloy. Mater. Des. 2024, 245, 113299. [Google Scholar] [CrossRef] [Scilit]
- Li, J.; Jie, W.; Yang, G. Effect of Gadolinium on Aged Hardening Behavior, Microstructure and Mechanical Properties of Mg-Nd-Zn-Zr Alloy. Trans. Nonferrous Met. Soc. China 2008, 18, S27–S32. [Google Scholar] [CrossRef] [Scilit]
- Li, J.; Jie, W.; Yang, G. Effect of Gadolinium on the Microstructure and Mechanical Properties of Mg-Nd-Zn-Zr Cast Magnesium Alloys. Rare Met. Mater. Eng. 2008, 37, 1751–1755. [Google Scholar]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.