1. Introduction
As easily beneficiated ore reserves become depleted and mining/geological conditions grow increasingly complex, technogenic mineral formations are becoming an additional source of mineral raw materials, and their processing is considered one of the priority areas for improving resource efficiency in the mining and metallurgical industry [
1,
2,
3,
4].
The accumulation of aged flotation tailings is accompanied both by losses of valuable components and by an increase in technogenic environmental load. In this regard, the processing of technogenic mineral formations is not only of economic but also of environmental importance and is consistent with the principles of rational subsoil use and the circular economy.
Long-term storage of tailings in open-air facilities leads to physicochemical changes, including surface weathering, the oxidation of minerals, and the formation of fine slimes and secondary minerals. These changes hinder the recovery of valuable components by conventional beneficiation methods. In particular, copper oxide minerals are difficult to recover by conventional flotation because of their strong surface hydrophilicity, fine particle size, complex mineral composition, and slime-related problems [
5,
6]. Therefore, the mineral-processing industry requires effective treatment processes and advanced technical support to selectively separate valuable minerals from gangue and harmful impurities [
2,
5,
7].
One promising approach is ultrasonic treatment. Ultrasonic treatment is considered an innovative physical–mechanical method for intensifying mineral-processing operations [
8,
9,
10,
11,
12]. In beneficiation, ultrasound is applied to pulp, i.e., a suspension of mineral particles in a liquid medium, to modify particle properties and interfacial interactions. Ultrasonic waves with frequencies above 20 kHz generate cavitation effects in the liquid, including the formation and implosion of microbubbles, as well as intensive acoustic microstreaming [
8,
9,
10,
11]. These effects can mechanically clean particle surfaces, destroy weak aggregates, improve dispersion of the solid phase, and even induce certain chemical transformations on mineral surfaces. Therefore, ultrasonic treatment is regarded as a promising green method for intensifying flotation and leaching: it is relatively simple to operate, does not require the addition of extra chemical reagents, and does not generate new pollutants. It is assumed that ultrasound can improve the reprocessing efficiency of aged tailings by activating mineral particle surfaces, removing interfering films, and thereby improving the recovery of residual valuable components [
8,
9,
10,
11,
12,
13].
Laboratory studies using ultrasound have demonstrated a positive effect on flotation performance. Videla et al. reported that ultrasonic treatment of copper flotation tailings improved copper recovery, which was attributed to the removal of slimes and oxide films from particle surfaces under acoustic cavitation [
13]. In contrast to previous studies, the present work focuses on aged copper-bearing tailings characterized by a very low copper grade (0.17 wt.%), a high proportion of oxidized copper forms (53.84%), and a substantial ultrafine fraction. In addition, the present study compares preliminary ultrasonic treatment after grinding with ultrasonic exposure during flotation, evaluates the effect of treatment duration over a wider range, and supports the technological results with statistical analysis and SEM observations. Aldrich and Feng showed that ultrasonic preconditioning of pulp can improve the flotation response of sulfide ores [
14]. Similar positive effects were reported for potash ore flotation [
15,
16], technogenic fluorite tailings [
17], chalcopyrite–pyrite separation [
18], galena flotation [
19], and the flotation behavior of calcite, barite, and quartz [
20]. Studies on coal flotation also showed that ultrasound can affect cavitation, bubble–particle interactions, and flotation performance [
21,
22,
23,
24]. In addition, Filippov et al. showed that ultrasound can influence flotation kinetics in a reactor-separator, indicating that acoustic treatment may affect not only particle-surface cleaning but also the rate of mineral recovery during flotation [
25].
An analysis of publications over the past two decades indicates sustained interest in the application of ultrasound in mineral processing. Based on review studies by Huan Zhang, Xiaoou Zhang, and co-authors, several important trends can be identified [
8,
9,
10,
11]:
Low-frequency ultrasonic exposure associated with transient cavitation is predominantly used as the main mechanism for intensifying flotation. This regime promotes active collapse of bubbles and cavitation nuclei, producing mechanical effects that remove slimes, destroy oxide layers, and improve reagent dispersion.
At the same time, high-frequency regimes (>50 kHz), under which stable cavitation forms and pronounced acoustic radiation are observed, remain insufficiently studied. However, such frequencies may significantly affect interactions between solid particles and air bubbles through acoustic aggregation and surface-property modification.
From a practical standpoint, the most important and technologically feasible approaches are ultrasonic treatment of ore pulp, which removes surface contaminants and fine fractions, and preliminary sonochemical modification of flotation reagents, which changes their rheological and surface-active properties and ultimately improves the selective recovery of minerals.
Studies can be conventionally divided into two main directions [
8,
9,
10,
11,
12,
21,
22,
23,
24]:
Preliminary ultrasonic activation, i.e., treatment of pulp or flotation reagents before the flotation process. This approach includes the study of improved dispersion and emulsification of reagents, removal of oxide films from mineral surfaces, and reduction in fine slime content under ultrasonic exposure.
Integration of ultrasound directly into the flotation process. In this case, attention is focused on the effect of ultrasound on bubble size and distribution, improved separation of gangue, and froth characteristics.
Thus, the development and implementation of alternative approaches for the reprocessing of technogenic tailings is an important task. Ultrasonic activation is considered a promising physical–mechanical technology capable of improving flotation efficiency by modifying interfacial interactions, improving reagent adhesion, and removing coating films. Despite the increasing number of studies on ultrasonic activation in beneficiation, its application to secondary resources, especially aged tailings, remains insufficiently studied, which confirms the relevance of the present work.
The studied tailings contain a significant proportion of oxidized copper forms. The flotation of copper oxide minerals is commonly associated with direct flotation, sulfidization flotation, or activation flotation [
5]. Sulfidization is widely used to improve the floatability of copper oxide minerals by forming active sulfide species or a sulfide film on the mineral surface, which promotes subsequent interaction with xanthate collectors [
5,
25]. However, the efficiency of sulfidization is strongly affected by pH, Eh, reagent dosage, mineral surface structure, and the presence of fine slimes [
5].
In our previous study, the same type of aged copper-bearing tailings was investigated with a focus on grinding-induced surface renewal, ORP changes, and sulfidization. It was shown that regrinding can renew mineral surfaces and improve flotation recovery, while excessive ultrafine grinding may intensify slime formation and reduce process selectivity [
26]. However, the potential of preliminary ultrasonic treatment as an additional physical method for the surface activation of these aged tailings has not yet been evaluated. Therefore, the present study continues this research direction by assessing the effect of ultrasonic treatment duration on copper flotation performance, supported by statistical analysis and SEM observations.
The aim of this study was to evaluate the effect of ultrasonic treatment on the flotation activity of copper minerals contained in aged tailings and to determine the most effective ultrasonic-treatment duration under the investigated conditions.
2. Materials and Methods
To address the stated objectives, a sequential methodology was implemented, including preparation of an experimental ultrasonic-exposure scheme with specified power and frequency and a range of treatment durations, preliminary and in-process ultrasonic treatment of flotation pulp, and statistical processing of the data. This structure provides a transition from the formulation of scientific problems and literature analysis to a reproducible laboratory procedure that can provide a basis for further scale-up studies.
The study was focused on legacy flotation tailings from porphyry copper ores stored in tailings facilities in the Republic of Kazakhstan. Due to long-term storage under atmospheric conditions, the tailings underwent weathering and oxidation, resulting in the alteration of sulfide mineral surfaces and the formation of secondary oxidized copper phases. Such surface transformations are typical for aged tailings and lead to reduced flotation activity of copper-bearing minerals. Therefore, preliminary ultrasonic treatment was considered in this study as a physical method for surface activation and improvement of copper recovery. Their chemical and phase compositions were determined by conventional silicate analysis, while the contents of copper and other elements were determined by ICP-OES (Agilent ICP 725ES, Agilent Technologies, Santa Clara, CA, USA). Mineralogical analysis was carried out on polished sections in reflected light using an OLYMPUS BX 53 microscope (Olympus Corporation, Tokyo, Japan), integrated with a SIMAGIS XS-3CU imaging system and SIAMS Mineral C7 software (version 7, SIAMS Ltd., Yekaterinburg, Russia). Furthermore, the particle size distribution was mapped using a FRITSCH Analyzette 22 laser diffraction analyzer and a CYCLOSIZER LF-11 (CNSP, Shanghai, China). Phase identification was finalized using a Bruker D2 Phaser diffractometer (Bruker AXS GmbH, Karlsruhe, Germany).
Before flotation, the aged tailings were ground in an MSHL-7 laboratory ball mill (7 L; Mekhanobrtekhnika, Saint Petersburg, Russia) operated at 75% of the critical rotational speed using steel balls as the grinding medium. Grinding tests were performed at different grinding times, and a grinding duration of 5 min was selected as the working condition for subsequent flotation tests. After 5 min of grinding, the flotation feed had a d50 of approximately 8.4 μm and a d80 of approximately 98 μm, with approximately 77%–80% of the material passing 71 μm.
The beneficiation process included preliminary conditioning of the ground pulp, followed by the addition of flotation reagents: sodium sulfide (Na2S, Hami Shi Donghong Chemical Co., Ltd., Hami, China) at 400 g/t as a sulfidizing agent, potassium butyl xanthate (PBX, Intelliprom LLP, Zhezkazgan, Kazakhstan) at 75 g/t as a collector, and methyl isobutyl carbinol (MIBC, commercial industrial sample supplied by the processing plant, Russia) at 20 g/t as a frother.
The grinding conditions and reagent dosages used in the ultrasonic flotation experiments were selected on the basis of preliminary optimization tests conducted on the same aged tailings. These tests included evaluation of grinding duration and the dosages of Na
2S and PBX. The selected baseline conditions were 5 min of grinding, 400 g/t Na
2S, and 75 g/t PBX. MIBC dosage was kept constant at 20 g/t throughout the flotation experiments and was not included in the optimization series. These parameters were kept constant in the present study to isolate the effect of ultrasonic treatment. The corresponding preliminary optimization results are provided in the
Supplementary Materials (Tables S1–S3).
Sodium sulfide was used as a sulfidizing reagent because sulfidization is a common method for improving the flotation response of oxidized copper minerals by forming active sulfide species on the mineral surface [
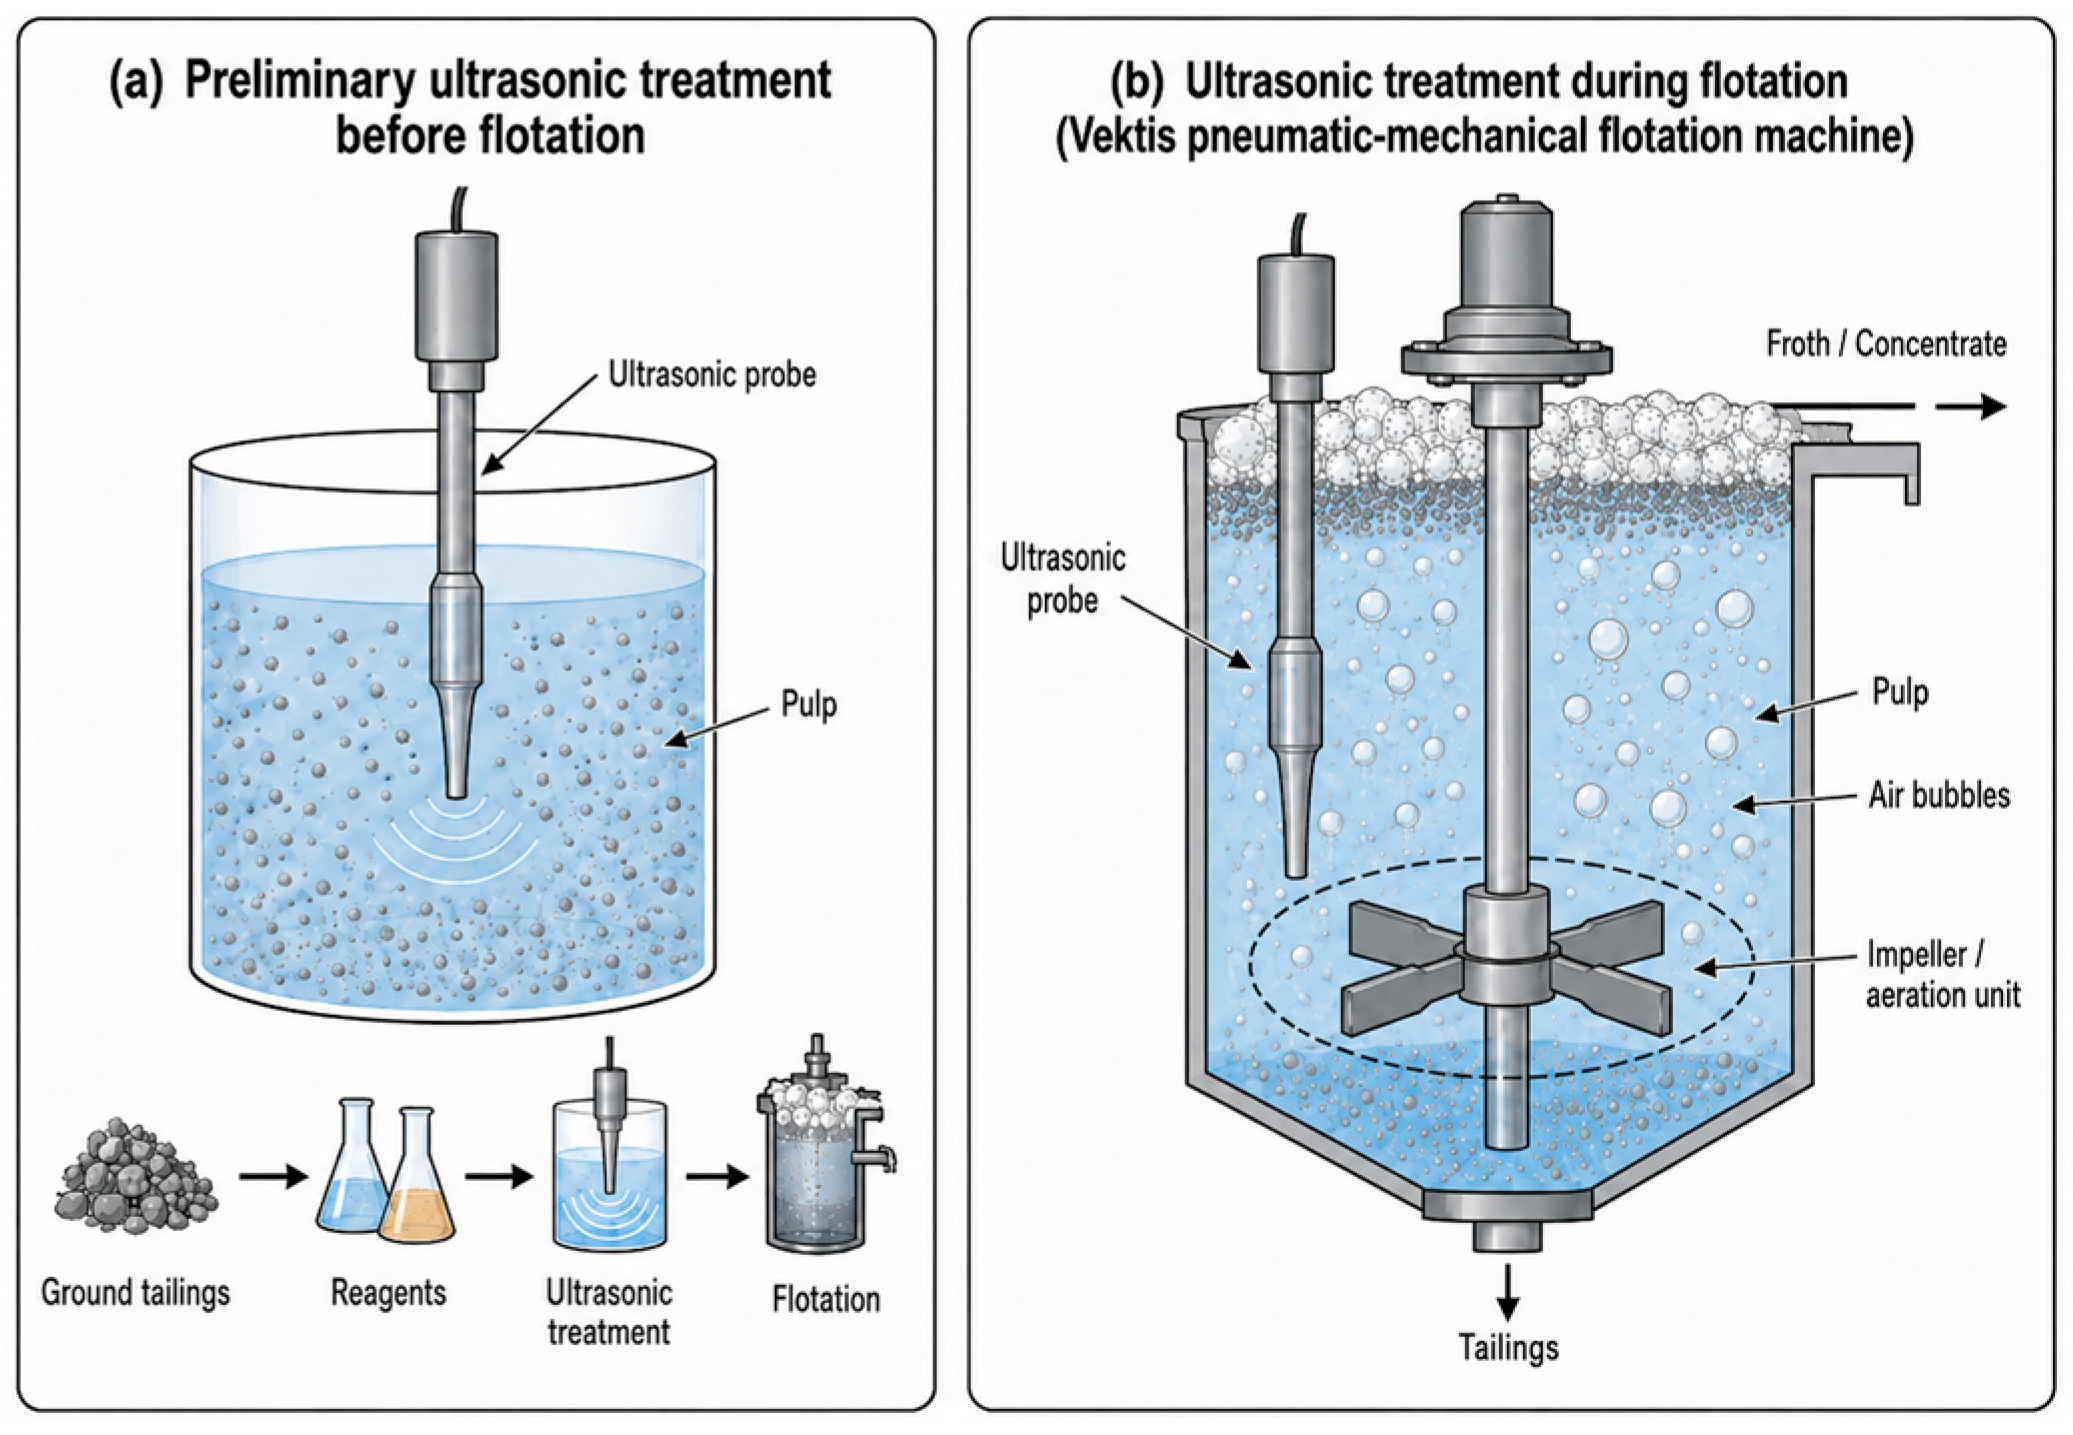
5]. This was followed by ultrasonic treatment under varied conditions. Flotation was then carried out for 5 min in a laboratory pneumatic–mechanical flotation machine. In the experimental series, the duration of ultrasonic exposure was varied from 0 to 25 min, both at the pulp-preparation stage and during flotation. Ultrasonic treatment was performed using an ultrasonic generator equipped with a probe immersed directly into the pulp. During preliminary ultrasonic treatment, the probe was inserted vertically from the top of the conditioning vessel. During ultrasonic treatment in the Vektis (Vektis, Saint Petersburg, Russia) pneumatic–mechanical flotation machine, the ultrasonic probe was installed vertically from the top of the flotation cell, adjacent to the central aeration unit, without touching the aeration unit or the cell walls. The arrangement of the ultrasonic probe during both treatment modes is shown in
Figure 1.
In the present study, two ultrasonic-treatment modes were evaluated: (i) preliminary ultrasonic treatment of the ground pulp before flotation, performed without aeration, and (ii) ultrasonic treatment applied directly during flotation. No desliming step or physical removal of a fine-size fraction was performed before flotation. Therefore, references to slime removal in this study refer to the partial removal or redistribution of fine surface coatings from mineral particles rather than the removal of ultrafine particles from the flotation feed.
The probe position was kept constant during all experiments in order to minimize the influence of geometrical factors on ultrasonic exposure. Froth height, bubble-size distribution, and froth stability were not quantified in the present study. Therefore, the possible influence of ultrasound on froth properties during in situ treatment was not evaluated separately.
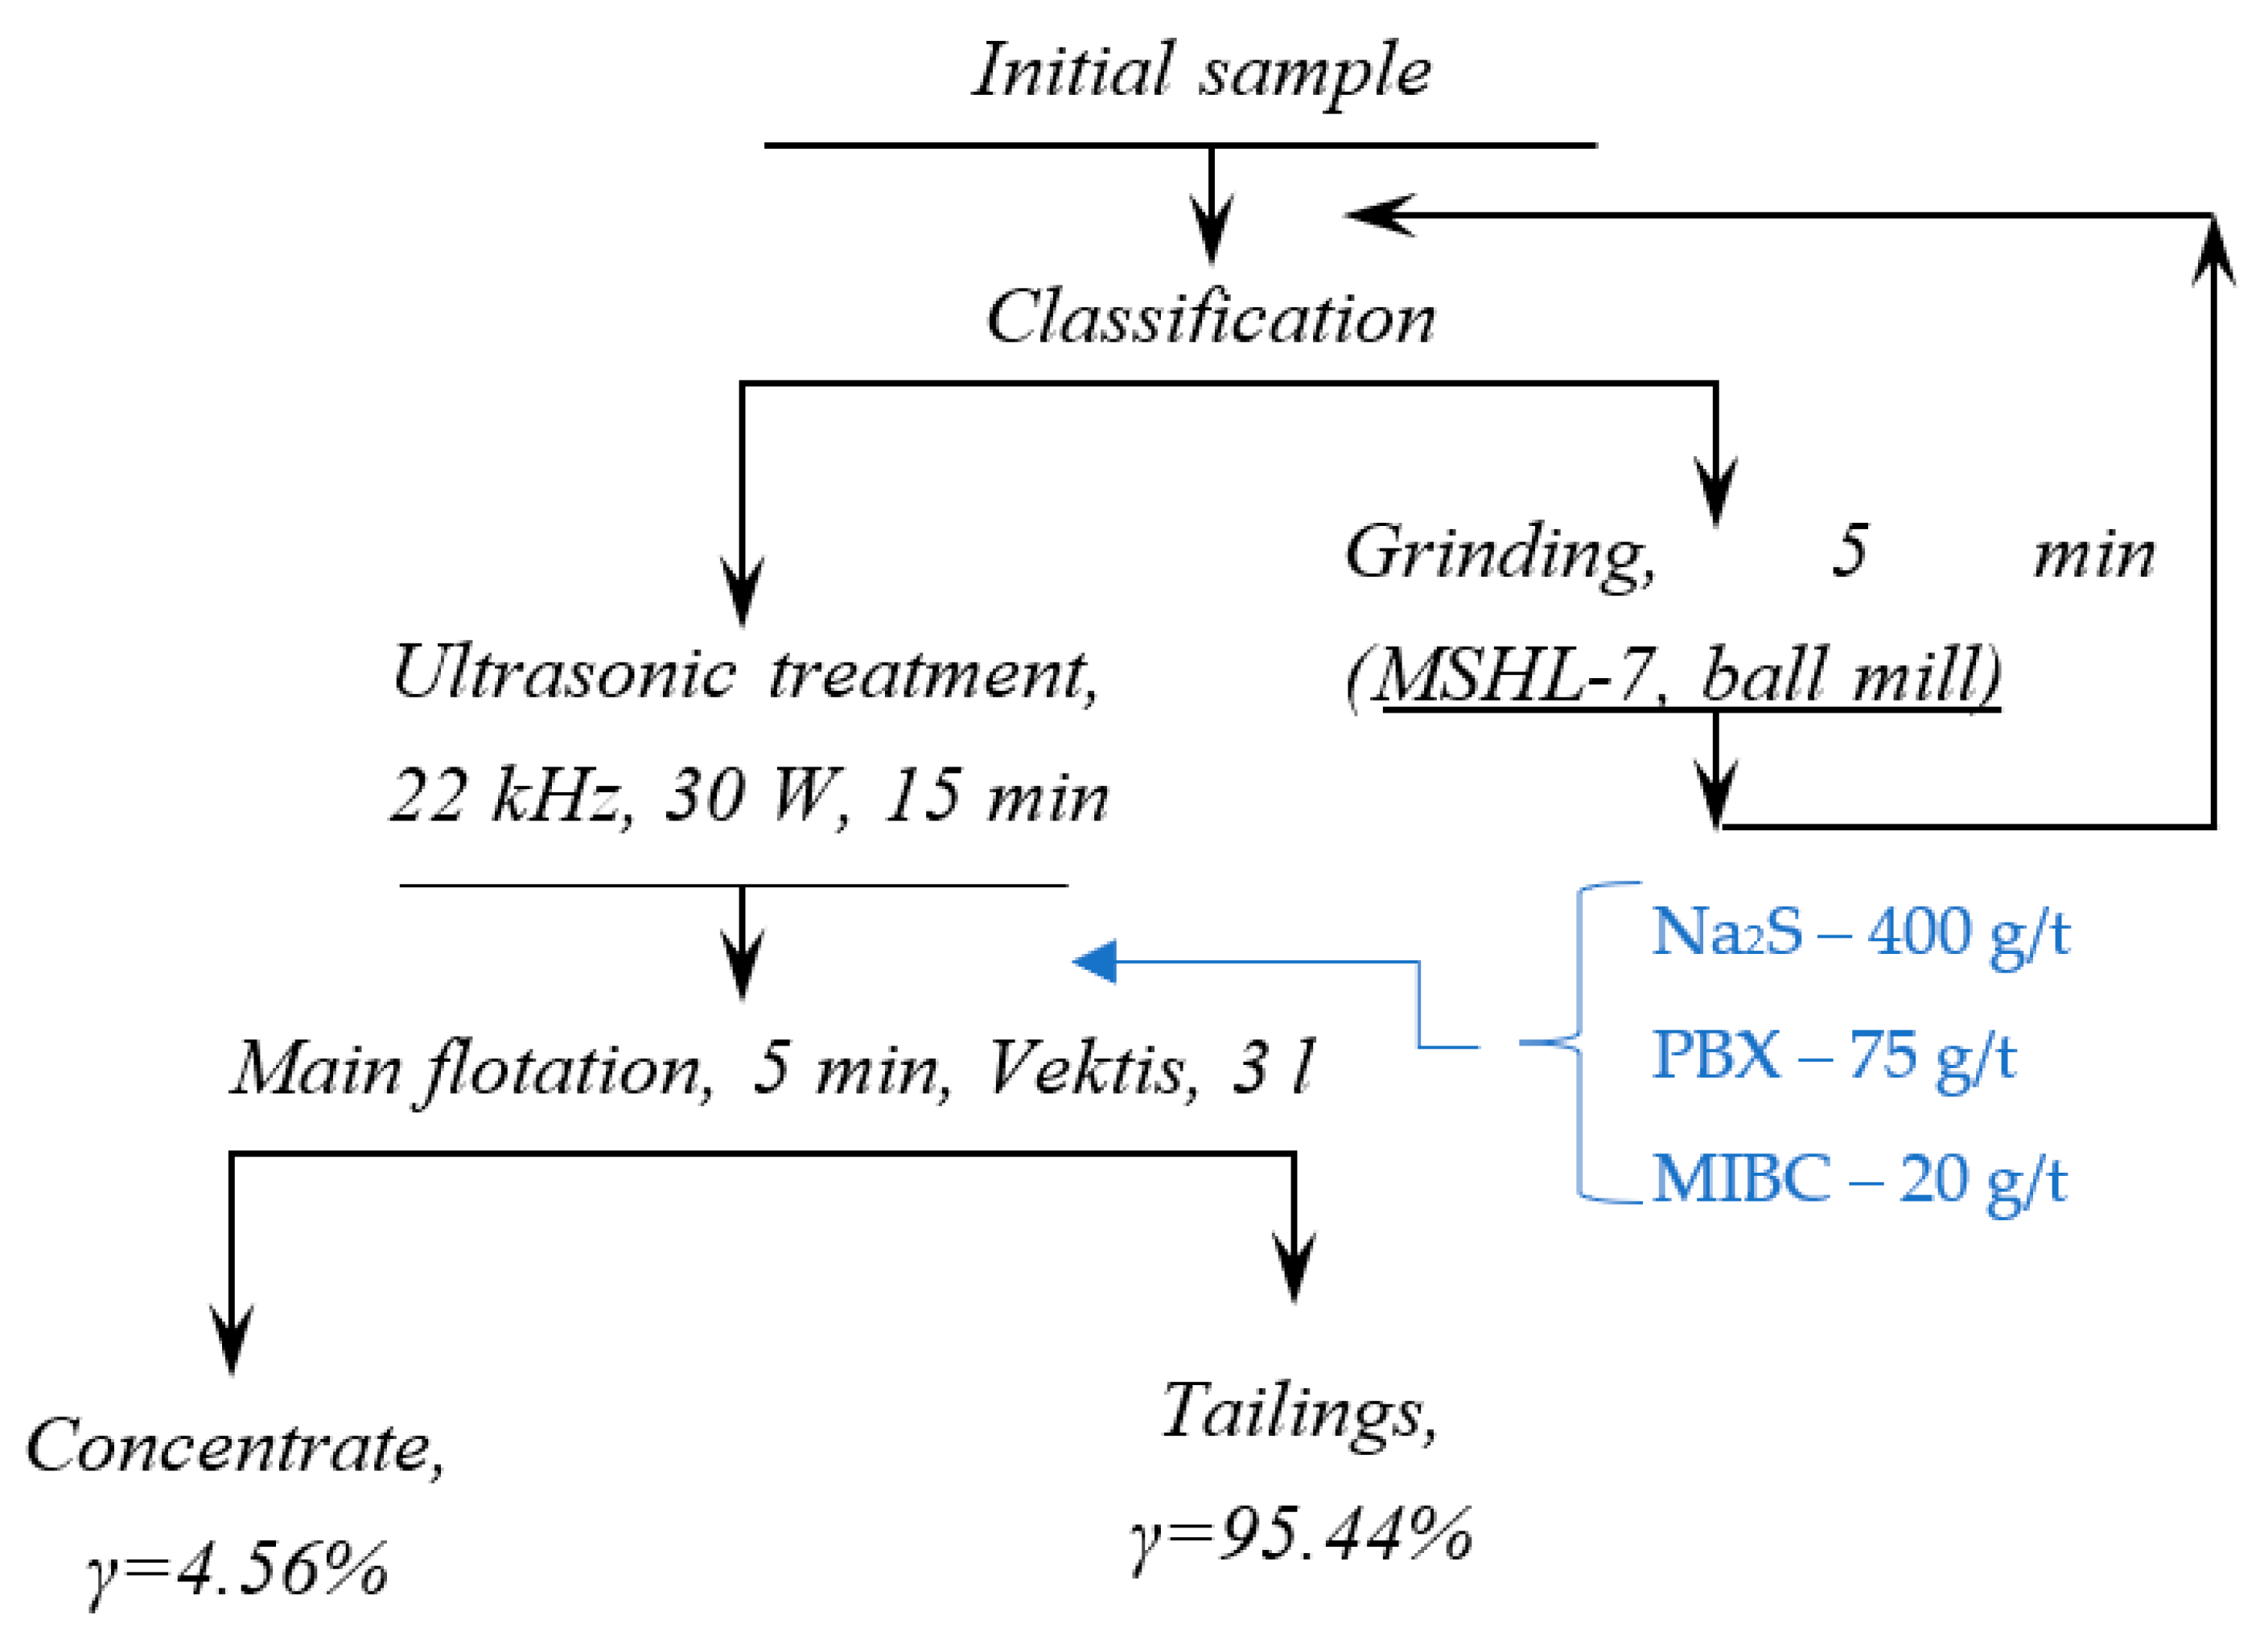
The technological scheme of the laboratory tests is shown in
Figure 2.
Figure 2 summarizes the principal operating conditions and product yields used in the main flotation experiment.
The main experiment was conducted at a pulp solids content of 30 wt.%, a feed copper grade of 0.17 wt.%, an ultrasonic frequency of 22 kHz, and a nominal ultrasonic power of 30 W. The volume of pulp subjected to ultrasonic treatment was 3 L, corresponding to a nominal ultrasonic power density of approximately 10 W/L. The actual acoustic power delivered to the pulp was not independently measured. During ultrasonic treatment, the pulp pH was 7.8–8.0 and the temperature was 25–26 °C. These parameters remained essentially stable throughout the experiments.
The flotation concentrates and tailings were analyzed for copper content, weighed separately, and copper recovery was calculated. The results were compared with control tests without ultrasonic exposure. The enrichment efficiency was calculated using the Hancock–Luyken formula:
where E is the enrichment efficiency (%), ε is the copper recovery into the concentrate (%), γ is the concentrate yield (%), and α is the copper content in the feed sample (%).
For statistical processing of the flotation-test results, one-way analysis of variance (ANOVA) was applied. The duration of ultrasonic treatment was considered as the independent factor, while concentrate yield, copper content, copper recovery, and enrichment efficiency were used as response variables. For the preliminary ultrasonic treatment after grinding, three replicate tests were performed for each selected regime, which made it possible to evaluate reproducibility and the statistical significance of the effect of exposure time.
The full range of exposure times (0–25 min) was first screened using single tests to identify the approximate region of best flotation performance; based on these preliminary results, four representative durations−0 (control), 15, 20, and 25 min—were selected for triplicate testing and subsequent statistical analysis, whereas the intermediate durations (2, 5, and 10 min) were evaluated only once and served solely for preliminary screening.
Consequently, the values reported for the preliminary screening series may differ slightly from the mean values obtained in the subsequent triplicate experiments. The screening data are presented as individual test results, whereas the replicated data are reported as mean ± standard deviation and were used for the statistical evaluation.
The significance of differences between regimes was assessed using Fisher’s F-test at a significance level of p < 0.05. The obtained results were used to identify the best-performing ultrasonic-treatment duration among the investigated conditions based on the maximum copper recovery and enrichment efficiency.
In addition, post-hoc pairwise comparisons were performed using Tukey’s Honestly Significant Difference (HSD) test (α = 0.05) to determine which specific duration groups differed significantly for each response variable.
Statistical analysis, including one-way ANOVA and Tukey HSD post-hoc comparisons, was performed using Microsoft Excel.
3. Results and Discussion
3.1. Characterization of the Aged Copper-Bearing Tailings
The results of this study include characterization of the initial mineral raw material, analysis of the chemical, phase, and particle-size composition of the aged tailings, and assessment of the effect of ultrasonic treatment on flotation performance. Special attention was given to comparing preliminary ultrasonic treatment after grinding with ultrasonic exposure directly during flotation. For the preliminary-treatment regimes performed in triplicate, mean values and standard deviations were calculated, and the statistical significance of the effect of ultrasonic treatment duration was evaluated using one-way ANOVA.
The principal chemical characteristics of the same tailings material, previously reported in [
26], are summarized in
Table 1 for reference.
As previously characterized [
26], the investigated material is a low-grade copper-bearing tailing containing 0.17 wt.% Cu. The matrix is dominated by SiO
2 and Al
2O
3, confirming the prevalence of silicate gangue. These compositional features are relevant to the present study because they define the mineralogical background against which the effect of ultrasonic treatment was evaluated.
The previously determined copper speciation of the same tailings is summarized in
Table 2 to provide the mineralogical context required for interpretation of the ultrasonic-flotation results.
Previous phase characterization of the same material showed that 46.16% of the total copper was associated with sulfide forms, whereas 53.84% occurred in oxidized forms [
26]. This high proportion of oxidized copper provides an important basis for evaluating the effectiveness of ultrasonic pretreatment in combination with sulfidization.
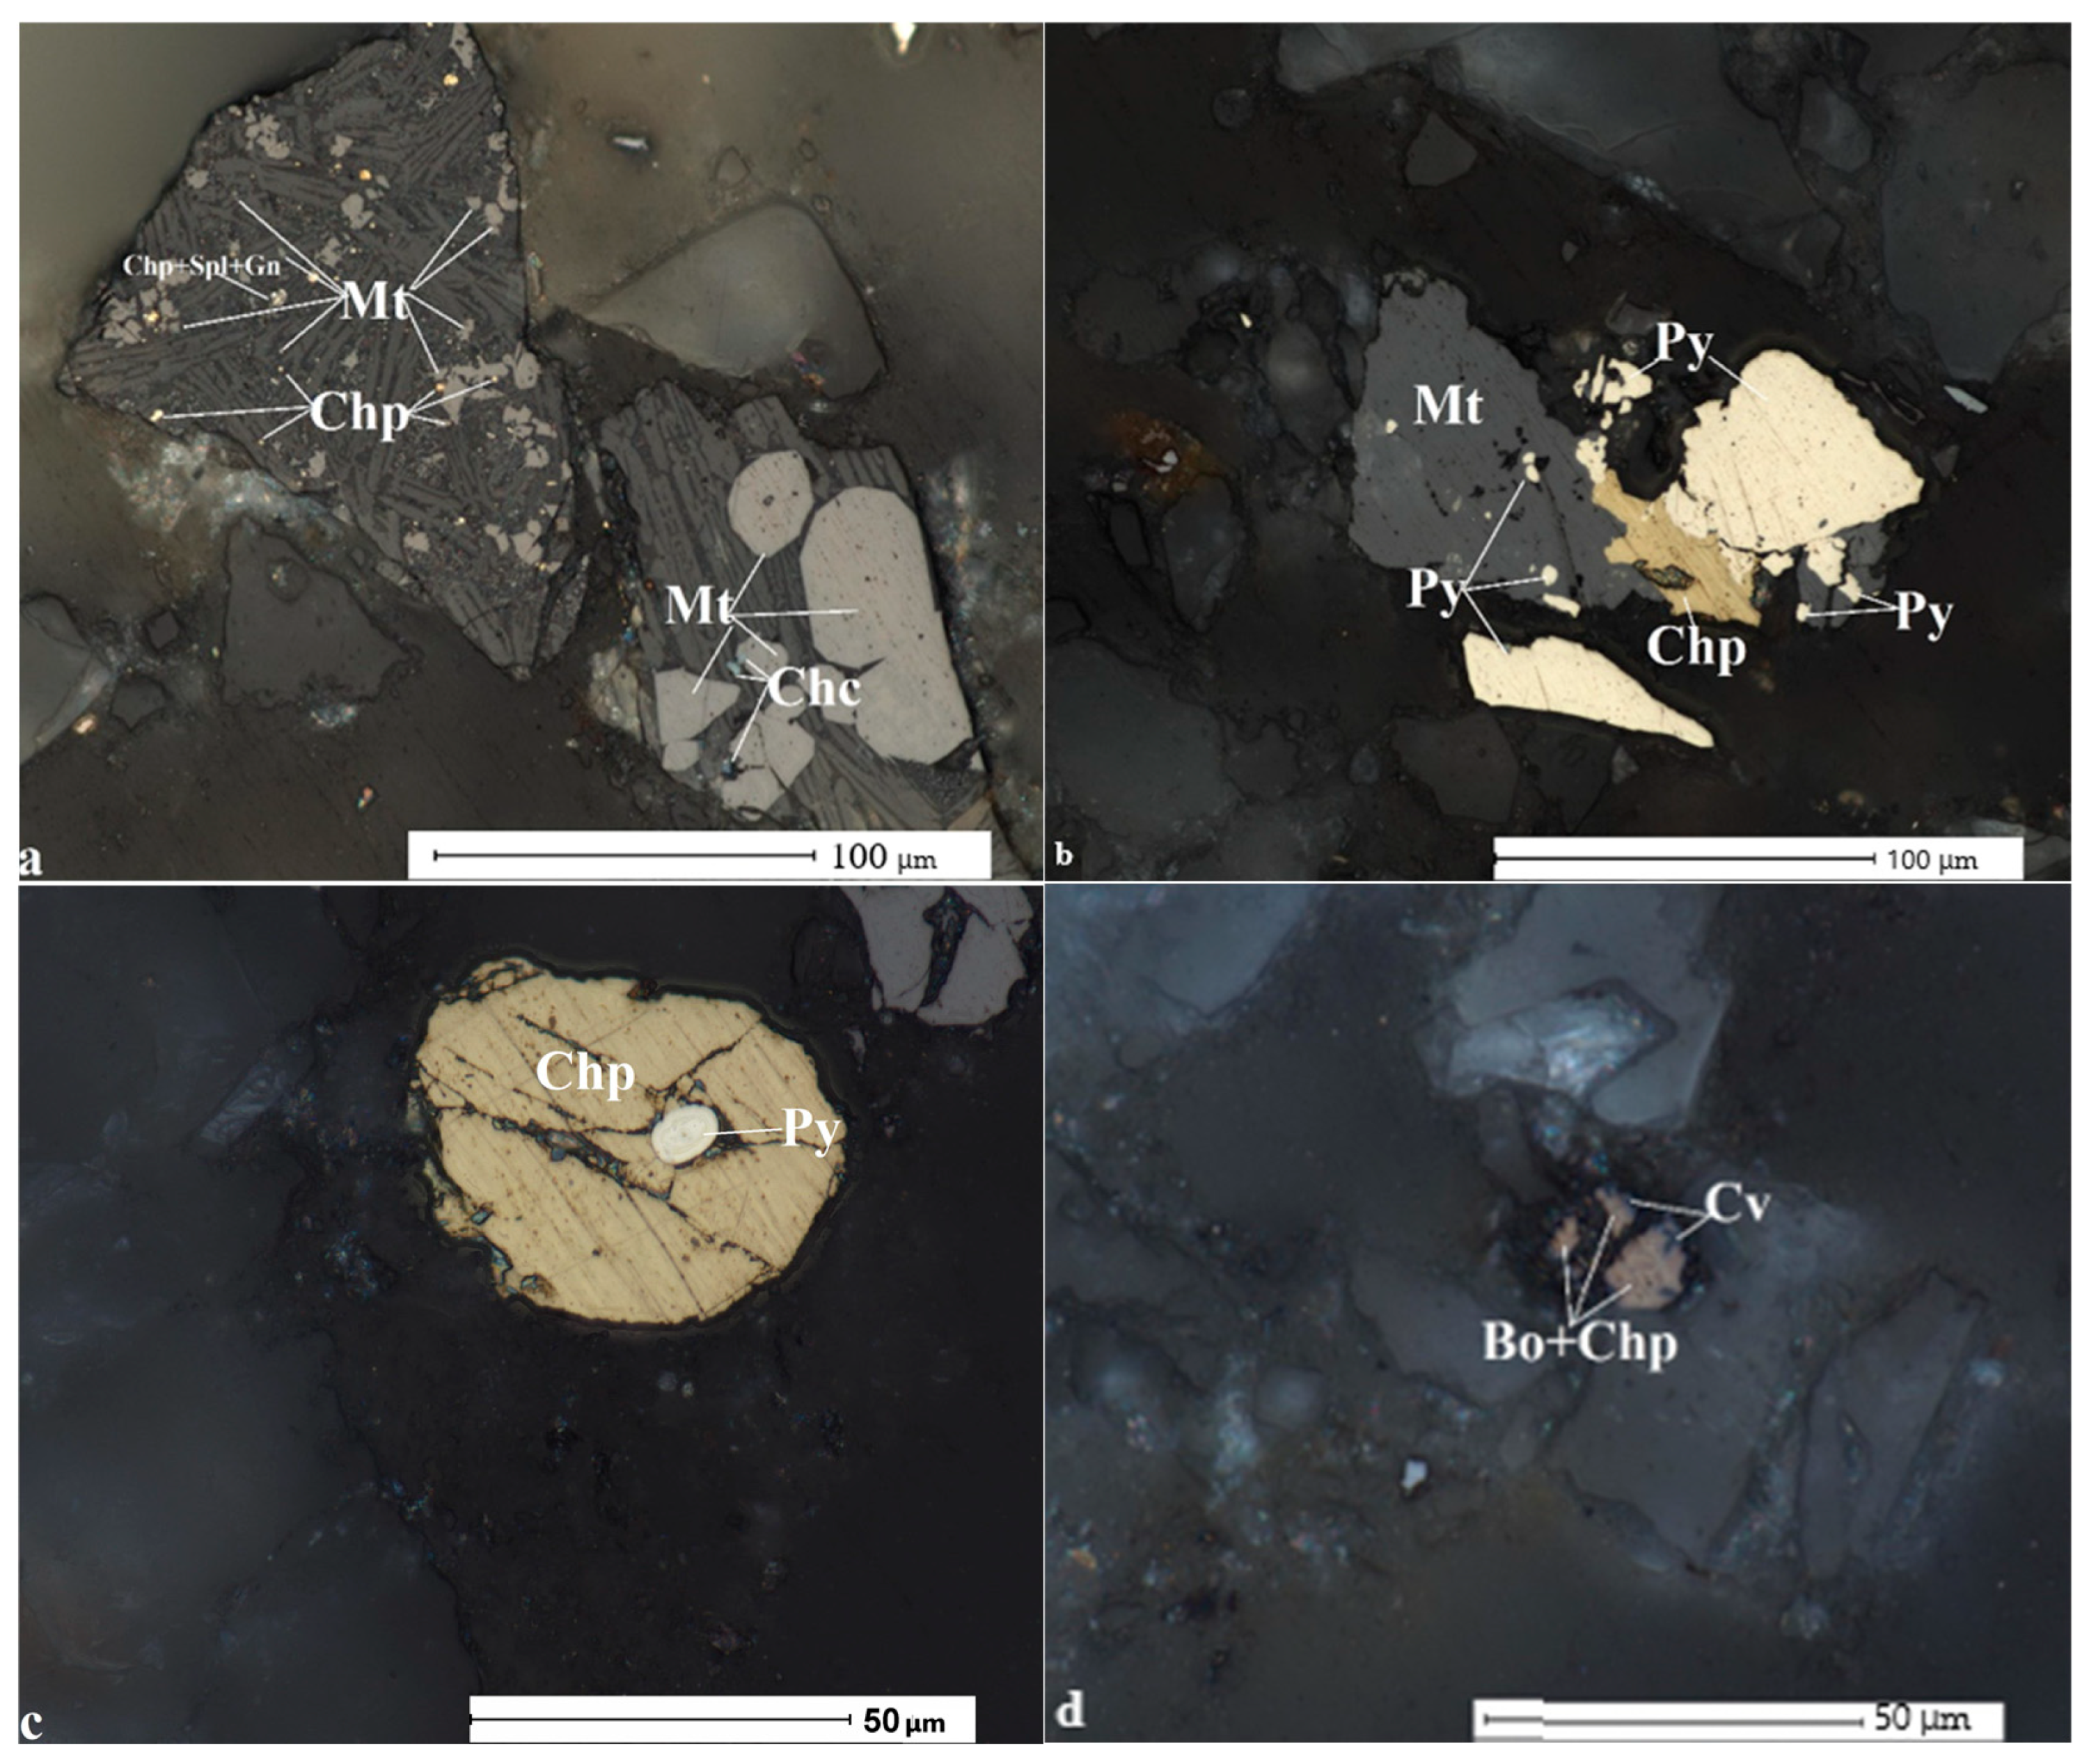
Optical microscopy confirmed that chalcopyrite is the principal copper sulfide phase in the aged tailings. It occurs in complex associations with pyrite, magnetite, and gangue minerals, while minor secondary copper sulfides, including covellite and bornite, were also observed (
Figure 3). Chalcopyrite occurs both as relatively liberated grains and as intergrowths with other mineral phases. Most chalcopyrite grains were within the fine and ultrafine size range, generally below 30 μm, although isolated coarser particles were also present. These textural characteristics are important for the present study because mineral associations and particle size may influence surface accessibility and the response to ultrasonic pretreatment.
In addition to chalcopyrite, minor secondary copper sulfides were identified. Covellite and bornite were observed locally, including a bornite–chalcopyrite association shown in
Figure 3c. These phases occurred less frequently than chalcopyrite and were therefore regarded as accessory copper-bearing minerals. Pyrite was also observed in association with chalcopyrite and gangue minerals (
Figure 3a,d). Because the present study focuses on the ultrasonic activation and flotation response of copper-bearing phases, the flotation behavior of pyrite was not investigated separately.
3.2. Particle-Size Distribution and Fine Slime Characteristics
The size-fraction distribution of the initial tailings sample, together with the Cu, Ag, and S grades and their distribution across individual size fractions, is presented in
Table 3.
The feed was characterized by a broad but fine particle-size distribution, with 51.66 wt.% below 45 μm and 73.42 wt.% below 71 μm [
26]. The absence of strong copper enrichment in any single coarse size fraction indicates that copper-bearing particles are widely distributed throughout the feed.
Because a large proportion of the feed was already present in the fine-size range, the −71 μm material was additionally characterized using a Cyclosizer. This analysis was used to resolve the ultrafine fractions more precisely and to determine how copper was distributed within the fine-particle population (
Table 4).
The data in
Table 4 highlight a significant challenge: the highest copper distribution (39.95%) is concentrated in the finest fraction (−8.4 + 0 μm), which accounts for 26.85% of the sample mass. From a metallurgical perspective, this may hinder flotation because ultrafine particles can promote slime-coating effects and interfere with the recovery of valuable minerals. However, no desliming was performed in the present study, and the full particle-size distribution was retained in order to evaluate ultrasonic pretreatment under conditions representative of actual aged-tailings reprocessing.
Size-fraction analysis of the flotation tailings showed a pronounced accumulation of ultrafine particles in the final tailings. The −8.4 μm fraction increased from 26.85 wt.% in the flotation feed to 41.01 wt.% in the tailings and accounted for 43.54% of the copper remaining in the tailings. This result indicates that the ultrafine fraction represents an important source of copper losses during flotation. The detailed size-fraction distribution of the flotation tailings is presented in
Table 5.
The results confirm that copper losses are preferentially associated with the ultrafine fraction. The accumulation of fine material in the flotation tailings indicates that ultrafine-particle behavior remains an important limitation to copper recovery under the investigated conditions.
3.3. Effect of Ultrasonic Treatment on Flotation Performance
The results of the laboratory experiment are presented in
Table 6.
Ultrasonic treatment had a nonmonotonic effect on flotation performance. The most effective regime was 15 min of exposure, at which the maximum values of copper recovery and enrichment efficiency were achieved. This improvement may be associated with particle disaggregation, dispersion of fine material, and possible partial cleaning of mineral surfaces under ultrasonic exposure.
Compared with conventional flotation without ultrasonic treatment, preliminary ultrasonic treatment for 15 min increased copper recovery from 40.56% to 44.12% and enrichment efficiency from 35.37% to 39.63%. Thus, the ultrasound-assisted flotation route provided a measurable improvement relative to the conventional control under otherwise identical reagent and operating conditions.
Phase analysis of the flotation products showed that copper recovered into the concentrate was derived from both sulfide and oxidized forms. The phase analysis presented in
Table 7 corresponds to the 15 min preliminary-treatment screening test reported in
Table 6. The concentrate contained 1.06 wt.% sulfide copper and 0.68 wt.% oxidized copper at a total copper grade of 1.74 wt.%. Thus, the numerical similarity between the overall copper recovery and the proportion of sulfide copper in the feed does not indicate exclusive recovery of sulfide minerals. The phase balance showed that oxidized copper also contributed to the recovered copper, although its recovery was lower than that of sulfide copper. The phase distribution of copper in the flotation products is presented in
Table 7.
The data confirm that both sulfide and oxidized copper contributed to the concentrate. However, a substantial proportion of oxidized copper remained in the tailings, indicating that incomplete recovery of oxidized copper forms was one of the principal limitations of the flotation process.
Further increasing the ultrasonic-treatment duration to 20 and 25 min did not improve the results. On the contrary, copper recovery and enrichment efficiency decreased. This trend may be related to excessive dispersion of fine particles, changes in particle–bubble interactions, or disturbance of the modified mineral surface during prolonged ultrasonic exposure. Since these mechanisms were not quantified directly, they should be regarded as possible explanations for the observed nonmonotonic response rather than as confirmed causes.
A comparison between preliminary and in situ ultrasonic treatment suggests that pretreatment before flotation was more favorable under the investigated conditions. This may be related to surface activation before reagent–mineral interaction. During in situ treatment, cavitation may also affect bubble–particle aggregates and froth behavior. However, because the in situ treatment series was limited and froth characteristics were not quantified, this comparison should be considered preliminary.
Because Na2S was used as a sulfidizing agent, the flotation response of oxidized copper minerals depended on the formation and preservation of sulfide-like surface species. It is therefore possible that prolonged ultrasonic exposure affected the stability of this modified surface layer. However, the present study did not directly characterize surface sulfur species before and after ultrasonic treatment, and this mechanism should be regarded as a possible explanation rather than a confirmed effect.
3.4. Statistical Evaluation of Ultrasonic Treatment Duration
To assess the effect of preliminary ultrasonic-treatment duration on flotation performance, one-way ANOVA was applied. The independent factor was ultrasonic exposure duration of 0, 15, 20, and 25 min. The experiments at 0, 15, 20, and 25 min were performed in triplicate. The response variables were concentrate yield, copper content in the concentrate, copper recovery, and enrichment efficiency. The results are presented as mean ± standard deviation (
Table 8).
Analysis of the mean values shows that the maximum copper content, copper recovery, and enrichment efficiency were obtained at a preliminary ultrasonic-treatment duration of 15 min. Under this regime, copper content in the concentrate was 1.79%, copper recovery was 44.37%, and enrichment efficiency was 40.06%. Increasing the exposure time to 20 and 25 min led to a decrease in technological indicators, indicating the nonmonotonic nature of the ultrasound effect.
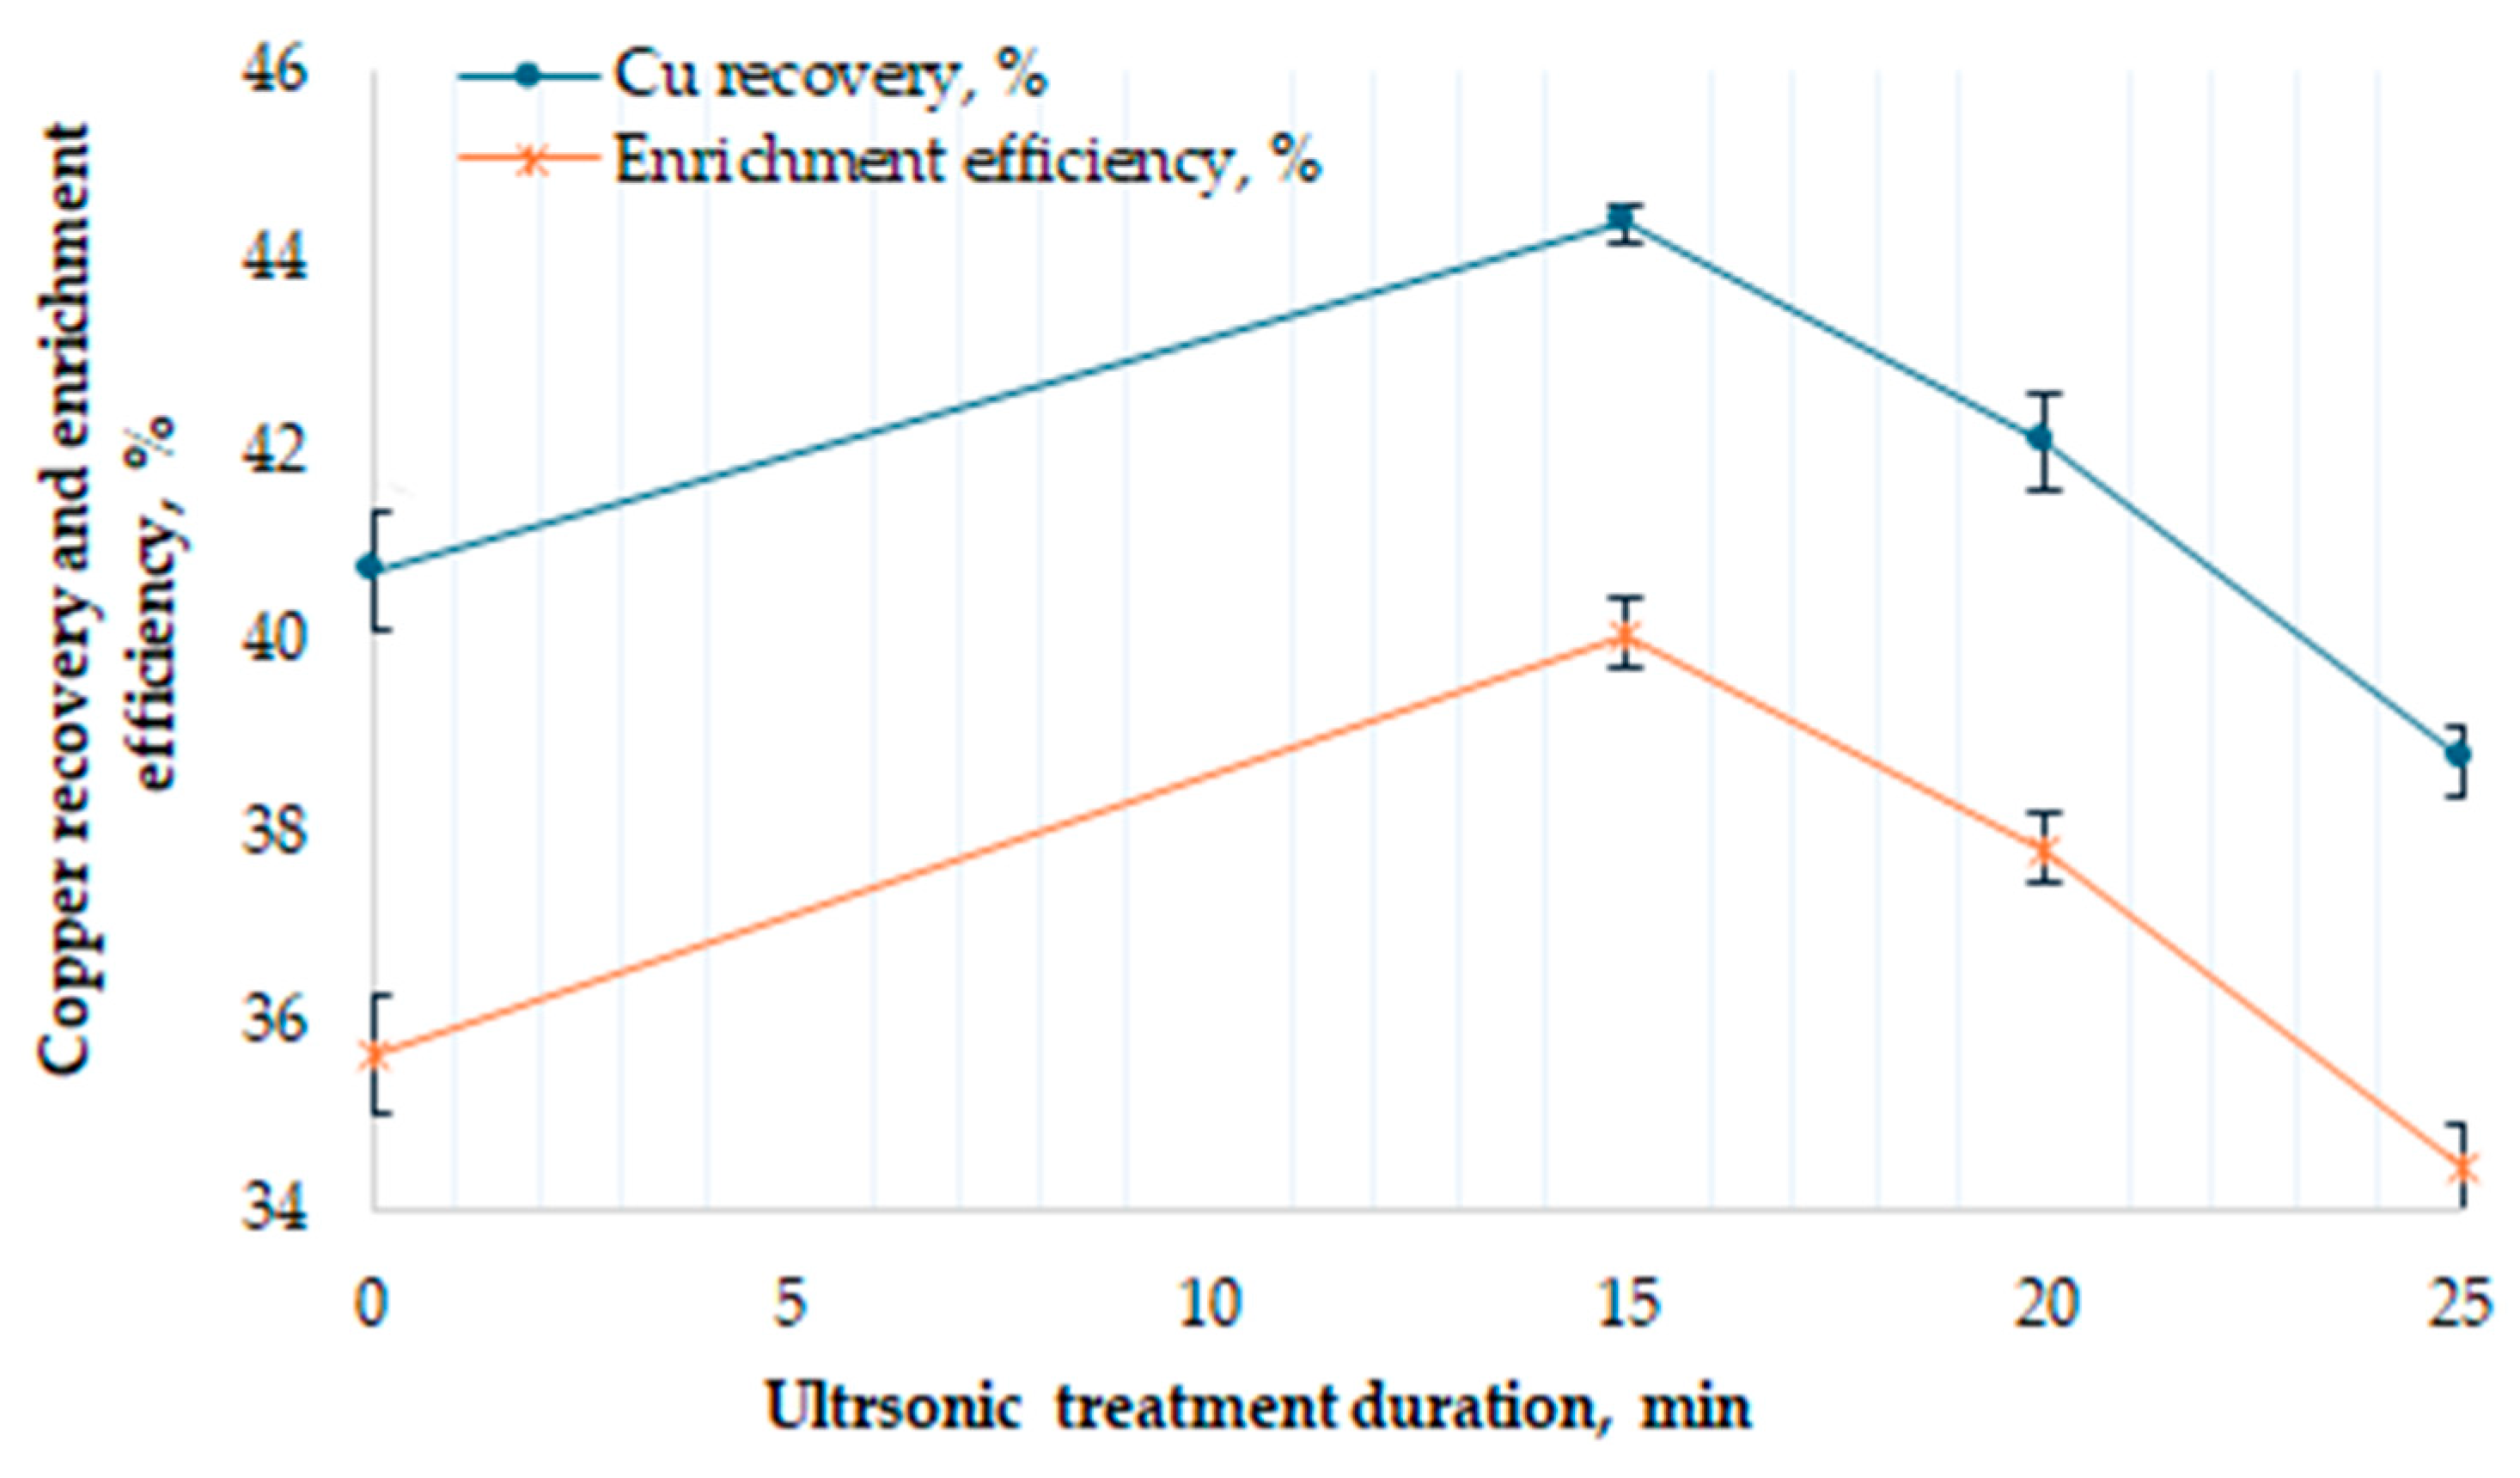
To better illustrate the nonmonotonic effect of ultrasonic treatment duration, the changes in copper recovery and enrichment efficiency are shown in
Figure 4.
As shown in
Figure 4, both copper recovery and enrichment efficiency reached their maximum values after 15 min of preliminary ultrasonic treatment and decreased at longer exposure times. This identifies 15 min as the best-performing ultrasonic-treatment duration among the conditions investigated. The results of the one-way ANOVA are presented in
Table 9.
The one-way ANOVA results showed that the duration of preliminary ultrasonic treatment had a statistically significant effect on all studied technological indicators, since p-values were lower than 0.05 for all parameters. The strongest effect was established for copper recovery and enrichment efficiency. These data identify 15 min as the best-performing duration among the tested preliminary ultrasonic-treatment conditions, providing the highest copper recovery and enrichment efficiency.
Post-hoc Tukey HSD comparisons (
Table 10) showed that the most pronounced differences at 15 min were observed for copper grade, copper recovery, and enrichment efficiency. Copper recovery and enrichment efficiency at 15 min differed significantly from the untreated control and from the longer treatment durations. In contrast, concentrate yield did not differ significantly between the 15, 20, and 25 min treatments. At 25 min, copper recovery was significantly lower than in the untreated control (
p = 0.003), whereas the difference in enrichment efficiency was at the significance threshold (
p = 0.050). The copper grade at 25 min did not differ significantly from the untreated control (
p = 0.093).
Laboratory tests were also conducted using a conventional flotation scheme consisting of rougher flotation and three cleaner stages in an open circuit. A copper concentrate with a copper content of 11.06% and a recovery of 41.93% was obtained.
Although preliminary ultrasonic treatment improved copper recovery, the overall recovery remained relatively low. These results indicate that further improvement should focus not only on concentrate upgrading but also on reducing copper losses to the tailings. Possible approaches include improved sulfidization of oxidized copper minerals, optimization of reagent dosage, better control of the ultrafine fraction, and the introduction of scavenger or closed-circuit flotation stages.
Based on the replicated experiments, 15 min of preliminary ultrasonic treatment increased mean copper recovery from 40.74 ± 0.63% to 44.37 ± 0.21% and enrichment efficiency from 35.65 ± 0.62% to 40.06 ± 0.38%. These results confirm that the improvement observed in the initial screening tests was reproducible. The decrease in copper recovery at longer treatment durations suggests that excessive ultrasonic exposure may adversely affect flotation performance. Possible reasons include increased fine-particle dispersion, re-aggregation of ultrafine particles, or changes in bubble–particle interactions; however, these mechanisms were not directly quantified in the present study. The results of the Tukey HSD pairwise comparisons are presented in
Table 10.
3.5. SEM Observations and Possible Mechanisms of Ultrasonic Action
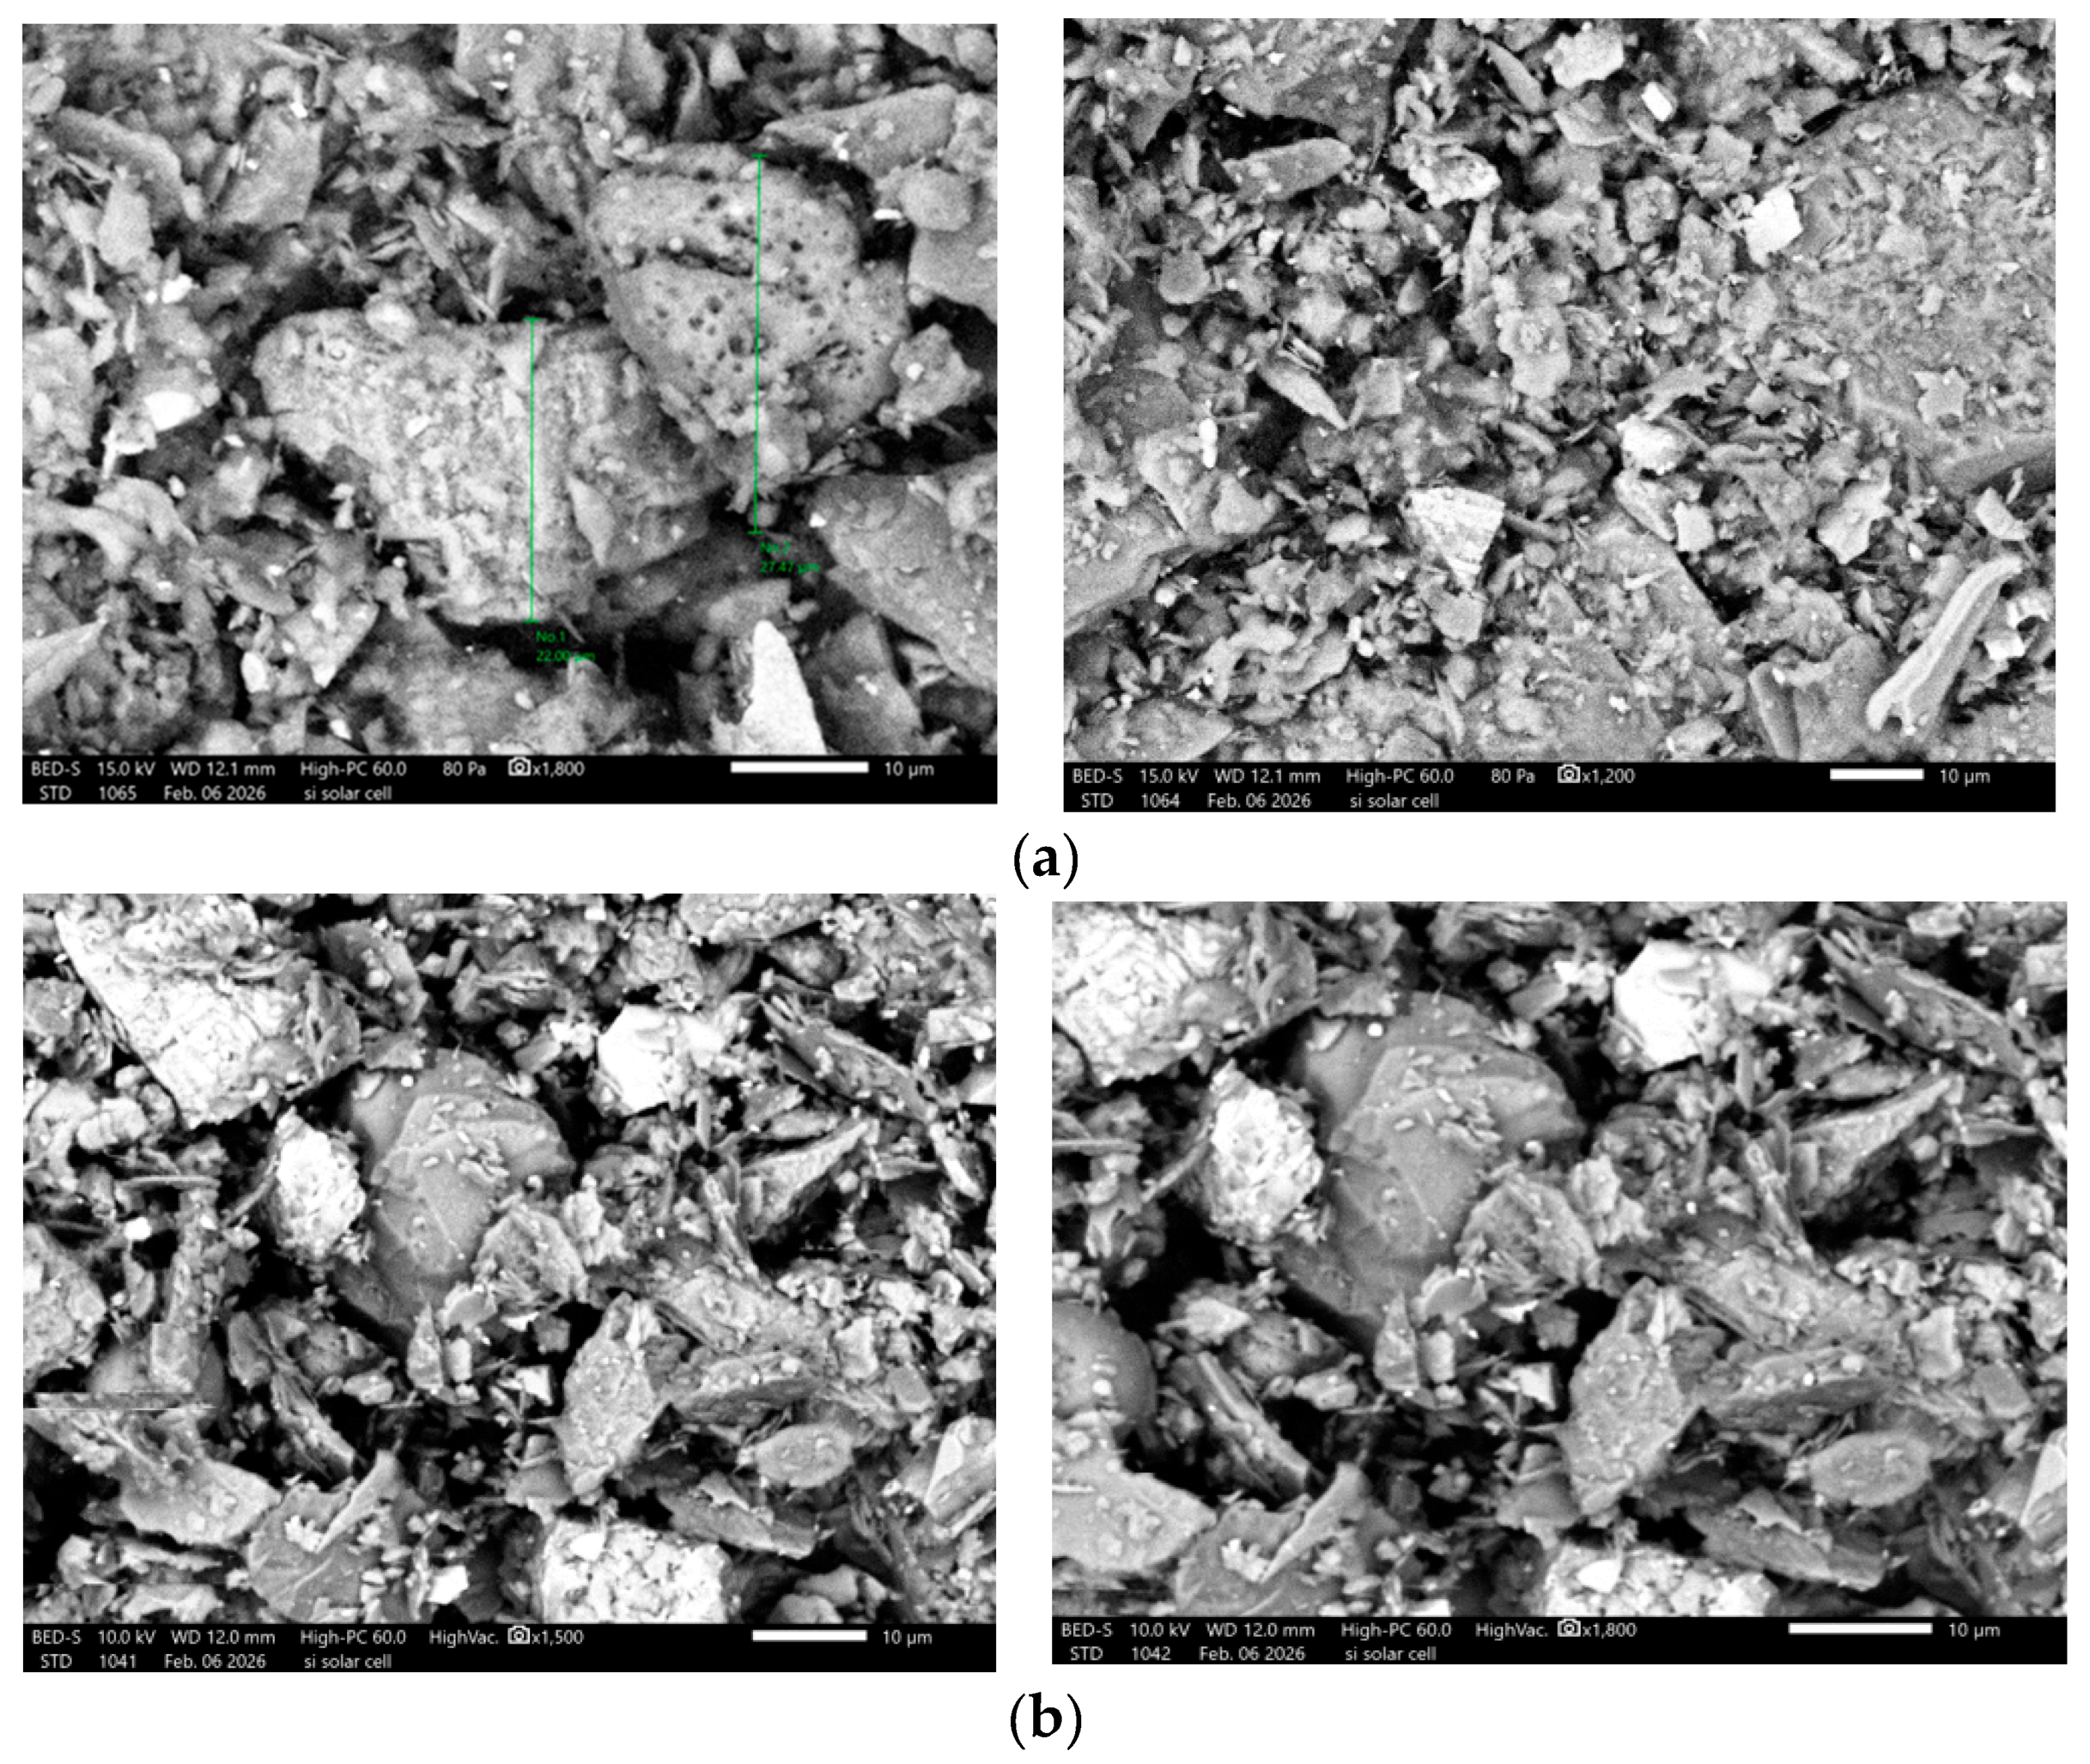
To examine possible morphological changes associated with ultrasonic treatment, SEM observations were performed on samples before and after ultrasonic exposure (
Figure 5). The untreated sample showed particle surfaces with accumulations of fine material, whereas after 15 min of preliminary ultrasonic treatment the examined particles exhibited more exposed surfaces and signs of disaggregation. These morphological differences are consistent with possible particle-surface cleaning; however, SEM observations alone do not provide direct evidence of slime-coating removal.
SEM observations revealed morphological differences between the untreated and ultrasonically treated samples. The untreated sample showed more frequent accumulations of fine material on particle surfaces, whereas the sample treated for 15 min exhibited more exposed and heterogeneous surfaces with signs of disaggregation. These observations are consistent with a possible surface-cleaning and dispersion effect of ultrasonic treatment; however, because different particles were examined before and after treatment, the SEM images should be regarded as qualitative supporting evidence rather than direct proof of slime-coating removal.
The SEM observations are consistent with the hypothesis that ultrasonic treatment promotes particle disaggregation and partial cleaning of mineral surfaces. However, the present data do not allow the individual contributions of surface cleaning, particle dispersion, reagent redistribution, and bubble-related effects to be distinguished conclusively. Therefore, the proposed mechanism should be regarded as a plausible interpretation rather than a directly demonstrated physicochemical mechanism.
In addition to its direct effect on mineral particles, ultrasonic cavitation may also influence the dispersion, transport, and adsorption of flotation reagents in the pulp. Enhanced mixing under acoustic microstreaming may improve reagent distribution and increase the probability of reagent–mineral contact. However, the individual contribution of these effects was not quantified in the present study and should therefore be considered as a possible additional mechanism rather than a confirmed explanation.
The present results do not allow a single dominant mechanism of ultrasonic action to be identified conclusively. The SEM observations mainly support particle disaggregation and partial surface cleaning, while enhanced dispersion of fine particles may also contribute to improved flotation performance. Possible effects related to micro- or nanobubble formation, reagent redistribution, and changes in bubble–particle interactions cannot be excluded; however, these phenomena were not quantified directly in the present study. Therefore, the observed improvement should be interpreted as the combined result of several cavitation-related effects rather than as evidence of one isolated mechanism.
Direct changes in particle-size distribution immediately before and after ultrasonic treatment were not measured in the present study. Likewise, the chemical state of the sulfidized mineral surface was not characterized directly; therefore, any discussion of ultrasound-induced changes in particle size or sulfidized surface stability should be regarded as a hypothesis requiring further verification.
A quantitative comparison with previous studies further clarifies the significance of the present results. Videla et al. reported an improvement in copper recovery of up to 3.5 percentage points after ultrasonic treatment of copper flotation tailings [
12]. In the present study, preliminary ultrasonic treatment for 15 min increased copper recovery from 40.56% to 44.12% in the screening tests, corresponding to an absolute increase of 3.56 percentage points, while the replicated tests showed a similar increase from 40.74 ± 0.63% to 44.37 ± 0.21%, i.e., by 3.63 percentage points. The magnitude of the recovery improvement is therefore of the same order as that reported by Videla et al. [
12]; however, the present study addresses a substantially different material system. In particular, the investigated feed contained only 0.17 wt.% Cu, with 53.84% of copper occurring in oxidized forms, together with a substantial ultrafine fraction. In addition, the present work compares preliminary and in situ ultrasonic treatment, evaluates a wider range of treatment durations, and demonstrates a statistically significant nonmonotonic response, with 15 min identified as the best-performing duration under the investigated conditions. Hassanzadeh et al. reported that ultrasonic treatment of porphyry copper ore increased chalcopyrite grade from 21.5% to 28.9%, although recovery slightly decreased from 86.4% to 84.8%; when an ultrasonic bath was combined with a homogenizer, chalcopyrite recovery increased to 88.8% [
15]. Gungoren et al. obtained a maximum galena microflotation recovery of 77.5% at 30 W and 2 min ultrasonic conditioning, although this result was obtained in a much simpler single-mineral system [
18]. These comparisons indicate that the effect of ultrasound strongly depends on mineralogical characteristics, feed properties, and the mode and duration of ultrasonic treatment [
12,
15,
18]. In contrast to the relatively simple or higher-grade systems investigated previously, the present work demonstrates a reproducible improvement in copper recovery and a statistically confirmed treatment-time dependence for low-grade, highly oxidized aged copper tailings containing a substantial ultrafine fraction.
4. Conclusions
The effect of ultrasonic treatment on the flotation of copper minerals from aged copper porphyry tailings was investigated. The studied material was characterized by a low copper content of 0.17%, a significant proportion of oxidized copper forms (53.84%), and finely disseminated copper-bearing minerals, which complicates their reprocessing.
Among the tested conditions, the best-performing regime was preliminary ultrasonic treatment after grinding for 15 min at a nominal power of 30 W and a frequency of 22 kHz. Under this regime, copper content in the concentrate was 1.79 ± 0.06%, copper recovery was 44.37 ± 0.21%, and enrichment efficiency was 40.06 ± 0.38%. Increasing the treatment duration to 20 and 25 min did not provide additional improvement and was accompanied by a decrease in performance.
One-way ANOVA confirmed the statistically significant effect of preliminary ultra-sonic-treatment duration on concentrate yield, copper content, copper recovery, and enrichment efficiency. SEM observations revealed morphological differences consistent with particle disaggregation and possible partial cleaning of mineral surfaces after ultrasonic treatment.
Thus, under the investigated laboratory conditions, preliminary ultrasonic treatment provided a reproducible improvement in copper flotation recovery from aged tailings. Further work should investigate the influence of ultrasonic power and frequency and confirm the mechanism of surface activation using SEM-EDS, contact-angle measurements, or zeta-potential analysis.
The present study was limited to open-circuit laboratory flotation tests. Closed-circuit testing was not performed and should be considered in future work to evaluate the stability of the ultrasonic-treatment effect under circulating-load conditions and to confirm the technological performance of the proposed flowsheet.


 ,