


Abstract
Industry 5.0 (I5.0) reframes industrial transformation by placing human-centricity, sustainability, and resilience alongside digitalisation, and by linking the twin transition to circular economy ambitions. While the post-2020 literature is expanding, implications for Manufacturing Systems are presented as fragmented principles, technologies, or isolated use cases, which complicates traceability from I5.0 goals to system-level requirements. This manuscript addresses this gap by consolidating the I5.0 discourse via a challenge-based synthesis and translating it into Manufacturing System implications using an evidence-mapping logic. Reported challenges are clustered into four topic groups (planet and society, products and consumption, production, people) and mapped to the four Manufacturing System pillars to expose evidence concentrations and gaps. Building on this bridge, a Manufacturing Systems’ challenges taxonomy is derived in three streams: (i) personalised and circular products, (ii) sustainable, flexible, human-centric Manufacturing Systems, and (iii) an education and skills paradigm for reskilling across industry and research ecosystems. A research agenda matrix highlights priorities in lifecycle information infrastructures, orchestration metrics, human–automation symbiosis, and governance at a system-of-systems scale. In the coded corpus (n = 30), evidence is denser in Manufacturing Systems and operations and competitiveness and people (22 and 23 papers) than in materials and processes and product, tooling, and assembly (7 and 10 papers).
1. Introduction
Industry 5.0 (I5.0) has emerged as a reframing of industrial transformation objectives, shifting emphasis from a predominantly technology-led view of Industry 4.0 (I4.0) to a socio-technical agenda that explicitly integrates human-centricity, sustainability, and resilience. In the European policy framing, I5.0 complements the I4.0 paradigm by asserting that industrial competitiveness should be pursued within planetary boundaries and with worker wellbeing treated as a core design requirement, not as an afterthought [1,2]. Operationally, this reframing changes what “good” looks like for manufacturing performance: beyond productivity and cost. Manufacturing Systems are increasingly expected to deliver decision-grade trade-offs across lifecycle impacts, resilience under disruption, and auditable human-centric outcomes (for example, safety, workload, agency, and accountability) [3,4]. This positioning also connects I5.0 to the twin transition, where digitalisation is expected to accelerate decarbonisation and resource efficiency, while the digital sector reduces its own lifecycle footprint [3,5,6]. In parallel, academic synthesis work has clarified that I5.0 is not simply the next “technology wave”, but a normative set of constraints and values that shape how enabling technologies (for example, digital twins, Industrial Internet-of-Things (IIoT), Artificial Intelligence (AI), collaborative robotics) should be selected, governed, and evaluated [2,3,7,8,9]. In this manuscript, “competitiveness” is therefore treated as multi-dimensional manufacturing performance (cost, quality, delivery, flexibility) pursued under explicit sustainability, resilience, and human-centric constraints, rather than as a narrow cost-efficiency objective.
Despite this convergence on high-level principles, the practical implications for Manufacturing Systems remain difficult to operationalise [2]. A substantial portion of the literature discusses I5.0 through conceptual perspectives, policy roadmaps, technology-oriented accounts, but often without a traceable link from broad I5.0 challenge areas to the concrete design and operating choices that define Manufacturing System performance [3,9]. This fragmentation is consequential because Manufacturing Systems are precisely the socio-technical enterprises where I5.0 must “cash out” operationally, namely, in how products are conceived for lifecycle responsibility, how production and logistics are orchestrated under uncertainty, and how human work is augmented, safeguarded, and continuously developed [10,11,12]. Manufacturing Systems research has long emphasised the need to treat production as an integrated system of product, process, organisation, and performance trade-offs [13,14]. Under I5.0, this integration must expand to include multi-criteria value (stakeholder outcomes), lifecycle transparency, circular operations, and human–automation symbiosis as first-class requirements rather than secondary constraints [1,2,8]. Moreover, the I5.0 “mass individualisation” ambition implies operating in high-variety contexts while preserving industrial efficiency and stability, which makes the Manufacturing Systems lens particularly salient when translating I5.0 principles into implementable architectures and operating models.
A second limitation in the current I5.0 discourse is that evidence is rarely organised in a way that makes research density and gaps explicit at the Manufacturing Systems level [3,15]. In other words, it is often unclear which I5.0 challenge topics are strongly supported by published work, which Manufacturing System dimensions they most directly inform, and where the knowledge base is still thin or mainly conceptual. This matters for both researchers and practitioners: Without an explicit mapping, it is hard to justify a coherent Manufacturing Systems’ challenge taxonomy, to prioritise research directions, or to translate I5.0 aspirations into actionable programmes for industrial deployment, especially in resource-constrained contexts. This yields a practical problem for Manufacturing Systems’ engineering: Teams face a rapidly expanding I5.0 discourse, but lack a traceable way to (i) interpret recurring “challenge statements” as system requirements, (ii) locate where the knowledge base is mature enough to guide design choices, and (iii) identify where empirical or architectural evidence is still missing.
Accordingly, this study is guided by three research questions: (RQ1) Which I5.0 challenges recur in the post-2020 discourse, and how can they be consolidated into a compact set of coherent challenge clusters? (RQ2) How do these clusters map to the Four Pillars of Manufacturing Systems, and where is evidence concentrated versus sparse? (RQ3) What Manufacturing Systems’ challenge streams and research priorities follow from that mapping, to support actionable and research-relevant direction-setting?
This manuscript addresses these issues by providing a traceable bridge from the broad I5.0 challenge landscape to a Manufacturing Systems’ challenge taxonomy and a forward research agenda. First, the post-2020 I5.0 corpus is analysed through a challenge-based lens and consolidates reported challenges into a small number of coherent clusters aligned with the twin transition and circular economy framing. Second, this consolidation is operationalised through an evidence-density mapping logic that relates I5.0 challenge topics to the four Manufacturing System pillars [15,16], making explicit where evidence concentrates and where gaps persist. Third, using this mapping as justification, the I5.0 challenges for Manufacturing Systems are derived and structured into three streams: (i) design, production, and supply competitiveness enabled by personalised and circular products (supported by lifecycle information infrastructures and traceability concepts); (ii) evolution towards sustainable, flexible, and human-centric Manufacturing Systems (with human-in-the-loop operating models and multi-criteria assessment), and (iii) an education and skills paradigm that enables continuous reskilling and human-friendly technology development across industry–research ecosystems. Finally, missing links and research priorities are consolidated in a research agenda matrix that highlights cross-cutting needs in measurement, governance, interoperability, and evidence of operational impact. The remainder of the manuscript is organised as follows: Section 2 consolidates and structures the I5.0 challenge landscape and presents the evidence-density map; Section 3 translates the mapping into three Manufacturing Systems’ challenge streams with associated implications; Section 4 discusses cross-cutting tensions, the resulting research agenda, and study limitations.
2. Industry 5.0 Challenges: Conceptual Framing and Evidence Mapping
As the literature on I5.0 expands, practical implications are frequently dispersed across policy positioning, technology roadmaps, strategy frameworks, and domain-focused syntheses, which makes it difficult to obtain a coherent view of what is challenging, why it is challenging, and how challenges relate to each other at the Manufacturing Systems’ requirements level [3,9]. This section therefore consolidates the I5.0 discourse, clarifies its links to the twin transition and circular economy ambitions [5,6,17], and synthesises the reported challenges into a structured map that will be translated into Manufacturing System implications in Section 3 [18,19,20]. In line with the Introduction, the aim is not to restate definitions, but to create a traceable bridge from recurring challenge statements to system-level implications. In this paper, the term “Manufacturing Systems” is used with a pragmatic boundary: It includes the plant-level system and its immediate operational interfaces to product engineering and supply-chain coordination, because I5.0 challenges often propagate across organisational and lifecycle boundaries rather than remaining within a single workstation or line.
To avoid a descriptive overview, a structured literature synthesis was adopted centred on “challenges”, interpreted as barriers, tensions, capability gaps, and trade-offs that must be managed to enact I5.0 principles in industrial practice [2,9]. This interpretation is consistent with a socio-technical view of Manufacturing Systems, where outcomes depend on the joint design of technology, work, organisation, and governance, and with resilience and human-centric design perspectives that treat disruption-handling capacity and quality of work as engineering-relevant requirements rather than externalities [2,9]. The evidence base combines peer-reviewed publications with selected authoritative institutional sources, prioritising contributions that articulate explicit implementation constraints, requirements, or assessment needs [3,17].
To strengthen transparency and rigour without positioning the manuscript as a protocol-driven review, the evidence map is built from a documented, challenge-centred corpus construction and a consistent coding logic. Sources were identified through broad database queries in major scholarly indexes (e.g., Scopus, Web of Science, IEEE Xplore, Google Scholar) for 2020–present, using “Industry 5.0” as the anchor term and combining it with challenge-related descriptors (for example, challenge, barrier, trade-off, resilience, human-centric, sustainability, circular economy, twin transition). All retrieved contributions were then assessed for eligibility based on content, rather than ranked by outlet or method: A source was coded if it contained explicit challenge, barrier, tension, capability-gap, or “how to overcome” statements relevant to I5.0 implementation; sources that mentioned I5.0 without articulating such challenge statements were not coded for the map. Duplicates were removed at the source level and non-substantive or purely promotional mentions were excluded. This is a challenge-centred evidence-mapping study and does not claim comprehensive coverage of all I5.0 publications, because inclusion depends on the presence of explicit challenge statements. The resulting challenge-centred corpus comprises 30 distinct publications (Appendix A, Table A1), which are multi-tag coded to (i) one or more challenge clusters (Section 2.2, Section 2.3, Section 2.4 and Section 2.5) and (ii) one or more Manufacturing System pillars (Section 2.6), enabling an evidence-density representation where each source may contribute to multiple cells.
2.1. The Emergence of I5.0
The European Commission’s 2021 report [1] positioned I5.0 as a complement to the I4.0 paradigm, explicitly stating that industrial development should pursue societal goals beyond jobs and growth, respect planetary boundaries, and place worker wellbeing at the centre of production [1,2]. This positioning is important because it changes the evaluation criteria of manufacturing progress, shifting from a narrow techno-economic lens towards a broader stakeholder-oriented value logic [2]. In parallel, the academic literature has attempted to clarify what is genuinely new in I5.0 relative to I4.0. A widely cited synthesis distinguishes “inception, conception and perception” dimensions, arguing that I5.0 should be seen as an extension of the long-running I4.0 transition, but with explicit normative pillars that constrain and guide technology adoption (human-centricity, sustainability, resilience) [7,9,15]. For Manufacturing System research, this implies that technology selection and deployment must be treated as a socio-technical design problem (integrating technology, work design, organisational arrangements, and governance), rather than as a purely technical upgrade path [3,9,21].
Recent syntheses and domain surveys reinforce that the I5.0 discourse remains heterogeneous, spanning enabling technologies (for example AI, digital twins, IIoT, collaborative robotics) as well as governance, values, and socio-technical design principles [2,3,8,9,22]. For the purposes of this manuscript, this heterogeneity is not treated as a weakness to be “resolved” by proposing yet another definition. Instead, it motivates a challenge-based synthesis: Within the post-2020 I5.0 discourse, what tensions and capability gaps repeatedly appear when organisations attempt to enact human-centric, sustainable, and resilient manufacturing in real industrial settings [2,3]? This challenge-centred lens is used in Section 2.2, Section 2.3, Section 2.4 and Section 2.5 to consolidate recurring challenge statements into coherent clusters, which are then mapped to Manufacturing System pillars in Section 2.6 to support the downstream structuring in Section 3.
Finally, the emergence of I5.0 in Europe is tightly coupled with the twin transition agenda, namely, the coordinated pursuit of the green transition and digital transition [3,23]. In practical terms, this coupling means that industrial digitalisation is expected to accelerate decarbonisation and resource efficiency, while the digital sector itself is expected to reduce its own environmental footprint (for example energy use, materials, and lifecycle impacts) [2,23]. This policy framing provides an explicit bridge between I5.0, climate objectives, and circular economy strategies [1,6,9,21], which is why the challenges mapped in Section 2.2, Section 2.3, Section 2.4 and Section 2.5 are presented as cross-cutting and mutually reinforcing rather than independent “lists” [2,3].
2.2. Planet and Society Related Challenges
The I5.0 paradigm places “planet and society” constraints upstream of manufacturing decisions, which turns sustainability from an operational add-on into a boundary condition for competitiveness [1,2,3,17]. This implies that Manufacturing Systems must align with broader societal objectives, including climate mitigation and adaptation [24], inclusive prosperity, and contribution to the United Nations Sustainable Development Goals [25]. In operational terms, the challenge is that sustainability performance can no longer be treated as external compliance; it must be incorporated into production-system design, KPI systems, investment decisions, and cross-functional governance across value chains [2,26].
A first cluster of challenges relates to climate and resource pressures. Climate change is increasingly associated with systemic risks that propagate through industrial value chains [24]. Translating this into Manufacturing Systems, the challenge is not only to improve relative efficiency (“doing better”), but to align production, energy use, and supply networks with decarbonisation trajectories, while maintaining resilience to disruptions [17,26,27]. This reframes sustainability as a boundary condition for system design, not a parallel initiative, and it makes trade-offs explicit (e.g., short-term productivity gains versus trajectory-aligned decarbonisation choices). This creates hard trade-offs between cost, productivity, flexibility, and decarbonisation requirements, and thus elevates the need for robust decision models rather than isolated “best practices” [2,28]. A related unresolved tension is that digitalisation can enable efficiency and transparency, but it can also contribute to rebound effects if capability gains simply increase throughput or complexity without reducing absolute impacts.
A second cluster concerns circularity and lifecycle responsibility. In the European framing, circular economy is central to achieving resource security and emission reductions, and it requires industry to move beyond linear “take–make–dispose” models [6,28,29,30]. This implies Manufacturing Systems must support closed-loop flows and lifecycle transparency [6], which in practice requires traceability, data continuity, and new capabilities to measure circularity outcomes (for example, recycled content, remanufacturing yield, and end-of-life recovery performance) across product categories and supply networks [28,29]. However, circularity outcomes often depend on system boundaries and measurement choices (what is counted, at which lifecycle stage, and across which actors), so “improvement” claims become fragile unless assessment models are explicit and auditable. The challenge is that these requirements often conflict with short-term cost optimisation and with existing factory performance metrics, and they demand cross-organisational coordination that many firms, especially SMEs, struggle to orchestrate [31,32].
A third cluster is social legitimacy and the evolution of the “industrial contract” with workers and communities. I5.0 explicitly positions the human as central, and it frames technology deployment as legitimate only if it augments human capabilities, improves quality of work, and supports societal wellbeing [1,11,17,33,34]. This translates into challenges around human-centred design, occupational safety, skills evolution, and equitable distribution of productivity gains. This is not merely a human-resources issue; it becomes a Manufacturing Systems design problem involving task allocation between humans and machines, human factors and ergonomics, safety, training, and governance of algorithmic decision support [8]. The challenge here is twofold: (i) to define measurable, auditable human-centric KPIs that can coexist with classical operational KPIs, and (ii) to operationalise “human-centricity” in engineering terms, so that it can be embedded into system requirements, procurement, and continuous improvement routines [1,8,11,33,34]. This is also an evidence challenge, because many proposed human-centric metrics are still weakly validated across contexts, which limits decision-grade adoption.
Finally, “planet and society” challenges are cross-cutting: They interact with product design, consumption patterns, production systems, and people-related issues. For this reason, they are treated in this manuscript as an overarching constraint layer that shapes the other challenge clusters discussed in Section 2.3, Section 2.4 and Section 2.5, rather than as an isolated topic list [17,27,29]. From an implementation standpoint, short-term barriers often relate to data availability and instrumentation, whereas structural challenges relate to governance, incentives, and cross-actor coordination (particularly salient for SMEs).
2.3. Products and Consumption Related Challenges
From an I5.0 perspective, “products and consumption” challenges sit at the interface between (i) rising expectations for personalisation, transparency, and lifecycle responsibility, and (ii) the need to operationalise circularity without compromising competitiveness [3,23,29]. In practice, this shifts the design target from a stand-alone artefact to an integrated product-service ecosystem, where value is delivered across the whole lifecycle and across multiple stakeholders [2,23,35]. A central unresolved tension is that personalisation tends to increase variety and configuration complexity, whereas circularity often benefits from standardisation, modularity, and predictable reverse flows, so the two goals must be engineered as a coupled design problem rather than pursued independently.
A first challenge is personalisation under circular constraints, meaning products must be adaptable to evolving user needs while remaining compatible with reuse, repair, refurbishment, and remanufacture logics [36]. This creates design tensions between modularity, durability, safety, cost and aesthetics on the one hand, and traceability, disassembly, and secondary-material compatibility on the other. Recent circular design research increasingly treats these trade-offs as multi-objective problems, requiring explicit optimisation across lifecycle impacts and value retention mechanisms [37,38]. In this framing, personalisation is not only a market feature; it becomes a lifecycle design variable that directly shapes reverse flows and end-of-life decisions. This also implies that “competitiveness” increasingly depends on lifecycle value retention, not only unit-cost efficiency.
A second challenge is lifecycle information continuity. Circularity depends on reliable product data (materials, configuration, usage, maintenance history, repairability) being accessible to the relevant actor at the relevant time. Without that, circular strategies remain “conceptually attractive but operationally fragile”, especially when products circulate across owners, service providers, and regions [39,40]. This is one reason why the Digital Product Passport (DPP) has become a prominent research stream since 2021, focusing on the structure, requirements, and adoption barriers of lifecycle product data, as well as the organisational implications of transparency and interoperability [18,39,40]. Current work also explores how DPP concepts can support value-chain coordination and end-of-life decision quality, while highlighting governance and implementation complexity [18,40]. A practical constraint is that DPP-enabled transparency can shift compliance and data-management burden onto manufacturers and suppliers, which can be disproportionately challenging for SMEs unless reference models and shared infrastructures reduce transaction costs.
A third challenge is cross-industry interoperability and scalable implementation. Even when lifecycle data is conceptually defined, companies still need implementable reference models that connect product identifiers, enterprise systems, and industrial data spaces [39]. Recent proposals connect DPP concepts with established interoperability artefacts such as the Asset Administration Shell (AAS), aiming to make DPP models reusable across sectors and supply networks [19,20]. This is particularly relevant for Manufacturing Systems that must handle mixed product portfolios and multi-tier supply networks with heterogeneous digital maturity. Here, the main risk is that interoperability remains “assumed” while governance (responsibility for data quality, access rights, auditability) remains under-specified, limiting real-world scalability.
Finally, I5.0 amplifies consumer and stakeholder scrutiny. The combination of digital transparency, societal expectations, and policy pressure increases reputational and compliance exposure [23,39,41]. Consequently, product strategies increasingly require credible data-backed claims and auditable lifecycle narratives, which feeds back into requirements for traceability, verification, and trustworthy information flows [18,23,40]. Overall, product and consumption challenges can be summarised as designing personalisation and circularity as a coupled problem, then instrumenting that coupling through lifecycle data continuity and interoperable information architectures [20,39]. In implementation terms, short-term barriers tend to be data readiness and integration effort, while structural challenges relate to governance, interoperability ecosystems, and incentive alignment across value-chain actors.
2.4. Production-Related Challenges
Production-related challenges translate I5.0’s sustainability, resilience, and human-centricity pillars into deployable Manufacturing System capabilities [2,3]. The central difficulty is that these pillars are not additive—they interact. For example, higher flexibility can increase complexity and energy demand, while higher transparency can create data burdens and cybersecurity risks [11,17]. In practice, “improvement” in one dimension can degrade another unless the operating model and measurement system explicitly manage the trade-offs (for example, flexibility versus energy intensity, or transparency versus information overload). Recent I5.0 road mapping work therefore stresses the need for explicit strategy and systems modelling rather than isolated technology adoption [2,3,17].
A first production challenge is mass individualisation with system stability. I5.0 inherits the I4.0 ambition of delivering high variety with near-mass-production efficiency, but now under stronger sustainability and resilience constraints [2,26]. Here, “near-mass-production efficiency” is used as shorthand for sustaining high-throughput and predictable performance under high-mix volatility (changeovers, scheduling instability, quality dispersion), rather than simply increasing automation. This requires reconfigurable capacity, rapid changeovers, and planning approaches capable of absorbing product mix volatility without excessive waste or instability. At the conceptual level, frameworks that integrate “smart, green, resilient, and lean” logics show that performance cannot be optimised in a single dimension, because the levers and trade-offs span operations, technology, and supply networks [3,42,43,44]. A recurring feasibility constraint is that these capabilities often assume digital maturity and change capacity that SMEs may not possess without shared infrastructure or staged adoption pathways.
A second challenge is closed-loop manufacturability as a system property. Circularity is not only a product design issue; it demands that production systems can manage reverse flows, variable quality returns, and disassembly or remanufacturing operations with operational predictability [29]. This pushes Manufacturing Systems toward IoT-enabled visibility, standardised lifecycle data, and decision rules that link production planning with end-of-life pathways [18,45]. Recent work on changeable closed-loop Manufacturing Systems highlights how “take-back uncertainty” and “reconfiguration needs” become first-order design drivers, not secondary considerations [28,46,47]. Operationally, the critical issue is stability under uncertainty, not only technical feasibility: Reverse-flow variability can amplify WIP, changeover losses, and quality risk unless explicitly designed into planning and control.
A third challenge is assessment models that are decision-grade. I5.0 pushes organisations to justify choices with structured performance models covering sustainability, resilience, and human-centric impacts [2,17]. However, measurement systems often remain fragmented (KPI silos, incompatible maturity models, inconsistent boundaries). Work on metamodels for assessment model design explicitly targets this gap, emphasising that evaluation artefacts must be constructed to support transition decisions, not merely to describe states [48]. Complementarily, strategic roadmap research highlights how sustainable manufacturing functions are interdependent and require coordination across governance, skills, business model innovation, and network integration [2,3,9]. This also implies a validation gap: Without agreed boundaries and repeatable metrics, multi-criteria “success” claims remain difficult to compare and hard to use for investment decisions.
A fourth challenge is resilience under twin-transition constraints. The twin transition implies that digitalisation should support environmental performance and climate action, rather than increasing resource intensity [6,17,23]. Manufacturing Systems must therefore internalise energy and resource constraints into production control, technology selection, and supply-chain design [2,28]. In practice, this implies a move from “digital enablement” to “digitally enabled sustainability”, where data architectures, analytics, and automation are designed with explicit ecological and social objectives [2,26]. A practical risk is that “more digital” can also mean more data movement, more cyber exposure, and more organisational burden, so resilience must include both operational disruption and digital-dependency risks.
In synthesis, production-related challenges concentrate on achieving mass individualisation through reconfigurability, making closed-loop strategies operational at scale, and building decision-grade assessment and governance mechanisms that balance the three pillars without drifting into technology-driven implementation [2,3,17]. For example, a factory attempting high-mix production with take-back flows must simultaneously (i) stabilise planning under volatility, (ii) maintain traceable lifecycle data for circular pathways, and (iii) demonstrate multi-criteria gains (energy, resilience, and human-centric outcomes) using auditable metrics, otherwise “I5.0 alignment” remains rhetorical.
2.5. People-Related Challenges
People-related challenges are the differentiating element of I5.0 compared to prior industrial paradigms: The Manufacturing System is expected to enhance human wellbeing, agency, and capabilities, while still delivering competitive performance. This implies that “human-centricity” must be operationalised as a set of system requirements and governance choices (work design, authority allocation, accountability, and measurable outcomes), not treated as an aspirational value statement. This implies that “human-centricity” cannot remain a value statement; it must be engineered into system architecture, work design, safety, and skills development [8,17,23,49].
A first challenge is human-centric system design and deployment. Human-centric manufacturing requires technologies that augment operators rather than displace them, and organisations that treat human capabilities as a strategic asset. Position papers on human-centric manufacturing argue that future systems need measurable, transparent, and trustworthy mechanisms for human–machine coevolution, including attention to cognitive workload, ergonomic risk, and meaningful work [8,50,51]. Synthesis evidence also emphasises that human-centricity in I5.0 requires empowerment and competence-development in parallel with digital and robotic deployment; otherwise, “human-centricity” is reduced to rhetoric [49,52]. A practical limitation is that many proposed human-centric indicators are still weakly standardised across contexts, which makes it difficult to compare interventions or to embed requirements into procurement and continuous improvement routines.
A second challenge is human–AI collaboration governance. As AI moves from analytics support to co-creation and decision augmentation, Manufacturing Systems need explicit collaboration architectures specifying roles, authority, and accountability across human, AI, and cyber-physical agents. Method-oriented work on I5.0 collaboration architectures underlines that the core design problem is not AI capability alone; it is the semantic and process-level integration that keeps humans empowered and “in control” [53,54]. This is directly relevant to Manufacturing Systems where planning, quality, and maintenance decisions increasingly blend human judgement and AI recommendations [53]. Operationally, this demands explicit “who decides what” patterns (for example, AI proposes schedules or quality dispositions under defined constraints, while humans retain override authority and accountability); otherwise, decision augmentation can drift into opaque automation.
A third challenge is safety and resilience in human-centric digital environments. Wearables, proximity sensors, and physiological monitoring can improve safety and wellbeing, but they also raise ethical, privacy, and trust questions [53,55]. Recent proposals such as Safe Operator 5.0 architectures illustrate how resilience and wellbeing monitoring can be structured in layered digital architectures, while implicitly highlighting governance requirements for data use, consent, and organisational legitimacy [11]. These issues matter because people-related acceptance often becomes the pacing item of implementation [17,55]. From a Manufacturing Systems perspective, this means that safety and wellbeing monitoring must be designed as a legitimate socio-technical subsystem (rules, consent, transparency, escalation procedures), not merely deployed as sensing technology.
A fourth challenge is skills, re-skilling, and ecosystem alignment. I5.0 requires blended competence profiles, combining digital fluency with transversal skills (creative problem solving, systems thinking, collaboration) [56,57]. Decision-model research on reskilling programmes emphasises that organisational context (culture, incentives, job design) materially affects reskilling effectiveness, so capability building is a socio-technical transformation rather than a training add-on [58,59]. In parallel, engineering education research argues that I5.0 requires curriculum designs and learning ecosystems that integrate industry, research, and societal needs more tightly than traditional models [60,61]. A remaining gap is linking competence-development mechanisms to measurable Manufacturing Systems outcomes (for example, reduced instability under high mix, faster recovery from disruptions, safer human–automation interaction), which would strengthen decision-grade adoption.
Overall, people challenges converge on engineering Manufacturing Systems that are safe, trustworthy, and empowering, while ensuring that skill ecosystems evolve fast enough to absorb the socio-technical complexity introduced by human–AI collaboration and circular, data-intensive operations [17,55,56].
2.6. Evidence Mapping Towards Manufacturing Systems Challenges
Manufacturing Systems can be framed as socio-technical production enterprises that integrate (i) materials and manufacturing processes, (ii) product, tooling, and assembly engineering, (iii) Manufacturing Systems and operations, and supply-chain/supplier-network coordination and (iv) manufacturing competitiveness, where people-related capabilities (skills, work design, and human factors) are embedded as core competitiveness enablers rather than an isolated pillar [16].
To bridge the broad I5.0 challenge landscape (Section 2.2, Section 2.3, Section 2.4 and Section 2.5) to Manufacturing Systems implications (Section 3), we follow the organising logic of evidence-gap maps, structuring the coded corpus into a matrix that makes research concentrations and gaps explicit across predefined dimensions [62]. Figure 1 therefore operationalises Section 2 into an evidence-density map that relates the four I5.0 challenge clusters (planet and society, products and consumption, production, people) in rows, to the four Manufacturing System pillars (in columns). Bubble size and the numeric labels indicate the number of distinct sources coded to each intersection using a multi-tag protocol (a source may contribute to multiple cells), based on the challenge-related publications cited in Section 2 and deduplicated at the source level (the 30 publications considered are listed in Appendix A, Table A1). Coding follows the challenge-centred eligibility rule stated in Section 2: A source is counted when it contains explicit challenge/barrier/tension/capability-gap or “how to overcome” statements, and it is mapped to all relevant cluster–pillar intersections it supports. Accordingly, the map represents evidence-density (where the discourse contributes challenge-explicit statements) rather than evidence quality or causal validation, which is treated as a limitation, discussed later.
Figure 1.
Evidence-density map linking Industry 5.0 challenge clusters to the Four Pillars of Manufacturing Systems, based on the 30 corpus publications of Section 2, listed and coded in Table A1 of Appendix A. Bubble size and blue intensity scale with the number of distinct sources coded to each intersection (multi-tagging allowed).
The resulting pattern supports three implications. First, products and consumption link strongly to product/tooling/assembly and competitiveness, driven by work on circular product information continuity, traceability, and Digital Product Passports as lifecycle enablers (as confirmed by [18,20,63]). These aspects are deployed in Section 3 under the challenge “Design, produce and supply competitively: Personalised and circular products”.
Second, production challenges concentrate in Manufacturing Systems and operations (and extend into competitiveness), reflecting the centrality of resilient, flexible operating models and decision-grade architectures for I5.0 deployment [2,3,64]. These aspects are deployed in Section 3 under the challenge “Evolve to sustainable, flexible and human-centric Manufacturing Systems”.
Third, people-related challenges concentrate in the competitiveness pillar (and connect to systems/operations), consistent with the view that skills, empowerment, and work design are pacing factors for I5.0 adoption rather than “add-ons” to technology programmes [8,56,57]. These aspects are deployed in Section 3 under the challenge “Nurture an I5.0 education and skills paradigm across industry–research ecosystems”.
3. Industry 5.0 Challenges for Manufacturing Systems
Building on the challenge clusters consolidated in Section 2 and the evidence mapping to Manufacturing Systems concerns, this section translates the coded corpus into three challenges. For each challenge, the analysis consolidates the dominant contribution types, from information infrastructures and reference architectures to orchestration concepts and competence-development mechanisms, to clarify what the literature is already delivering and which requirements remain under-specified from a systems perspective. To strengthen operational anchoring, each stream is also discussed in terms of (i) how it manifests in shop-floor and value-chain decisions (for example, planning and control, quality loops, data governance, and human–automation task allocation), and (ii) which issues are short-term implementation barriers versus longer-term structural constraints.
3.1. Personalised and Circular Products: Integrating Tracking Features and Lifecycle Adaptability
Manufacturing Systems should remain competitive while products become simultaneously more personalised (variant-rich, customer-specific, frequently reconfigured) and more circular (durable, repairable, upgradable, remanufacturable, recyclable). In practice, competitiveness shifts from efficient output to efficient lifecycle value, which makes product-level traceability and auditable lifecycle records a functional requirement for design, production, service, and end-of-life decisions. The coded corpus therefore converges on DPP-like information backbones, where the product is treated as a physical artefact with a governed digital identity, supported by unique identification, sustainability-relevant data structures, event histories across actors, and stakeholder-specific access under explicit governance, which in turn creates a systems-integration problem across PLM, production, supply chain, and aftermarket information flows (Figure 2).
Figure 2.
DPP-enabled lifecycle information backbone for personalised and circular products. Grey arrow represent the closed-loop physical lifecycle (design to recovery pathways). Blue and green arrows represent the bidirectional information exchange between lifecycle events and the DPP, enabling decision-making for personalisation updates, service actions, and circular routing (repair, remanufacture, recycle).
Recent publications contributing to this challenge can be organised into five complementary contribution streams.
The first stream focuses on problem framing and design space, consisting of definitions, requirements, and research agendas for passports. Van Capelleveen et al. [63] propose a structured conceptualisation of product/material passports and synthesise the research space, clarifying boundaries, attributes, and an agenda for passports as a decision-enabling interface across circular supply chains. Lopes and Barata [18] review DPP research and explicitly position DPPs as lifecycle data mechanisms to reduce information asymmetries that hinder circular strategies, while outlining open issues around standardisation, governance, and implementation pathways. Complementing these perspectives, Wicaksono et al. [65] provide a systematic literature review focused on DPP technological advancement and adoption, highlighting practical barriers (scalability, stakeholder coordination, legal/economic constraints) and proposing an adoption-oriented conceptual model. Together, these works give a traceable rationale for why Manufacturing Systems must treat DPP-like mechanisms as part of the operational architecture, not as a reporting add-on.
The second stream addresses the required data and how to structure it, consisting of data standards and templates for circular product information. Mulhall et al. [66] introduce the Product Circularity Data Sheet as a standardised “digital fingerprint” concept intended to harmonise circularity data exchange across supply ecosystems, emphasising the need for common fields and trust mechanisms to make product circularity data actionable. In a related “data realism” contribution, Çetin et al. [67] analyse data requirements and availabilities for material passports and expose typical data gaps and stakeholder-specific needs, reinforcing that circular traceability is as much an organisational and data-collection challenge as it is a technical one. For Manufacturing Systems, these works are important because they translate “track the product lifecycle” into concrete data categories that must be captured, validated, updated, and made accessible.
The third complementary stream focuses on how to implement interoperable DPP-like infrastructures, by presenting reference architectures and implementations for lifecycle passports. A notable line of work implements DPP concepts using interoperable industrial data structures. Plociennik et al. [19] present an end-to-end approach for a DPP concept (Digital Lifecycle Passport) explicitly designed to serve multiple stakeholders including end-of-life actors, and they rely on the AAS to structure and share lifecycle information. Kühn et al. [20] also focus on DPP implementation and explicitly combine DPP requirements with AAS-based modelling choices, contributing to the engineering question of how “passport objects” can be integrated into industrial interoperability stacks. These implementation-oriented studies reduce ambiguity around how passports can be embedded into industrial systems, which is essential if Manufacturing Systems are to operationalise circularity and personalisation without collapsing into bespoke integrations.
A fourth stream concerns maintaining the continuity and decision-usefulness of lifecycle data, proposing digital-thread and digital twin (DT) approaches for sustainable PLM. Because personalisation and circularity increase lifecycle variability, the Manufacturing System needs mechanisms to maintain a coherent “story” of each product instance. Biachini et al. [68] review the digital-thread concept, positioning it as an approach for lifecycle data continuity across tools and actors. In parallel, Seegrün et al. [69] review sustainability-focused DT applications across lifecycle phases, emphasising how DTs can increase transparency and enable data-driven sustainability interventions. Mügge et al. [70] systematise how digital twins can support circularity across lifecycle stages, reinforcing the role of DT/PLM linkages as enablers of sustainable lifecycle decisions rather than purely operational monitoring. For the present challenge, these works collectively support the idea that DPPs become significantly more valuable when connected to digital-thread/twin mechanisms that keep lifecycle data current, contextualised, and decision-ready.
Turning lifecycle data into competitive choices is the last complementary stream concerning the decision support for circular design and lifecycle assessment. On the “decision layer”, Ortner et al. [37] propose computational multi-objective optimisation for circular economy product design, clarifying how optimisation can help manage trade-offs among circularity objectives (waste, impact, reuse potential) in realistic design spaces. Turner et al. [35] propose the concept of dynamic LCA enabled by intelligent products, explicitly connecting lifecycle data availability to improved end-of-life decisions and circularity performance. These contributions are central for competitiveness because they show how lifecycle tracking can move beyond compliance into systematic design and operational advantages.
Across these publications, the field is converging on the notion that personalised and circular products require a product identity, lifecycle record, interoperable data model and a decision layer (Figure 2). Evidence is also accumulating that adoption bottlenecks are not purely technical; they include data governance, certification/trust, confidentiality, and usability for non-expert humans, especially in multi-tier supply chains and end-of-life contexts [18,65,67]. From a Manufacturing Systems viewpoint, these bottlenecks show up as concrete operational failure modes (missing or untrusted lifecycle attributes, inconsistent identifiers, access-right conflicts, and “data latency” that makes passport information obsolete at the moment of decision). For Manufacturing System research, this points to a clear gap: how to integrate passport/digital-thread mechanisms into production planning, quality, and service operations in a way that (i) is lightweight enough for broad industrial uptake, (ii) remains interoperable across ecosystems, and (iii) demonstrably improves both circular outcomes and competitive performance. For example, when a returned product instance is scanned at goods-in, DPP status variables (configuration, usage history, and certified component condition) can drive a routing decision (repair, remanufacture, harvest for parts, recycle), which must then be reflected in finite-capacity scheduling, quality disposition rules, and inventory policies, without collapsing into manual exception handling.
3.2. To Evolve to Sustainable, Flexible and Human-Centric Manufacturing Systems
Manufacturing Systems should be designed and governed to deliver sustainability, resilience, and human-centricity simultaneously, treating them as coupled design objectives that must be operationalised in planning and control across the plant and its supply-chain/supplier-network interfaces. Across the coded corpus, flexibility and resilience are approached as architectural properties under volatility, while human-centricity is treated as an engineered socio-technical requirement, which together shifts Manufacturing Systems decision loops towards multi-criteria performance and human-in-the-loop patterns (Figure 3). A practical implication is that “decision-grade” adoption depends on explicit trade-offs and measurable criteria (for example, energy intensity and scrap for sustainability, recovery time and schedule stability for resilience, ergonomic risk and workload for human-centricity); otherwise, systems drift into technology-led implementation.
Figure 3.
Human-centric sustainable and resilient Manufacturing System framework, showing the coupling of multi-criteria performance, adaptive orchestration, and human-in-the-loop decision patterns enabled by digital architectures.
The recent literature contributes to this challenge through four main complementary streams, which together build a plausible “solution space” for sustainable, flexible, and human-centric Manufacturing Systems evolution.
System paradigms for flexibility and resilience under volatility is one of those streams. A core response is to move from rigid line-centric configurations toward structures that can be reconfigured quickly, both physically and logically, while preserving operational coherence. ElMaraghy et al. [13] articulate the long-term Manufacturing System trajectory toward more adaptable system concepts, which aligns with I5.0’s emphasis on robustness and responsiveness. More recently, Leng et al. [64] consolidate decentralised manufacturing and autonomous manufacturing into a “Decentralised Autonomous Manufacturing” (DAM) paradigm, providing a reference architecture and explicitly positioning DAM as an I5.0 route to resilience. Complementarily, Wang et al. [71] propose an I5.0-oriented reconfigurable matrix-structured Manufacturing System, emphasising multi-variety, variable-batch production with human–machine collaboration, and detailing a roadmap (order feature analysis, cell formation and layout, multi-dimensional reconfiguration) validated through case and simulation. These works shift flexibility from local scheduling heuristics to architectural capability, meaning the system is designed to absorb variability through modularity, distributed decision-making, and reconfiguration logic. From an implementation perspective, a short-term barrier is instrumenting distributed visibility (data availability, interoperability), whereas a structural challenge is governance of distributed decision rights (what is local autonomy versus centrally constrained policy).
Another stream is the human-centric system design and “human–automation symbiosis” architectures. Human-centricity becomes actionable when embedded in Manufacturing System design methods and digital architectures. Peruzzini et al. [10] propose a Smart Manufacturing System Design framework explicitly grounded in human–automation symbiosis, targeting I5.0 system behaviour where humans and automation co-evolve through data, models, and AI-enabled support rather than substitution. At the production and logistics system level, Grosse et al. [72] synthesise the shift from Industry 4.0 to 5.0 through a human-centric lens, and argue for more systemic, empirically grounded and multimethod approaches that incorporate human factors and ethical implications into design and management. These contributions are consistent with the “operator-centred” framing in I5.0 and provide a defensible bridge from principles to design choices (task allocation, decision rights, interfaces, training, and performance measures). Therefore, human-centricity is treated as a design variable (work organisation, cognition, safety, autonomy), not just a human resources or change-management topic. Concretely, “human-in-the-loop” needs explicit authority allocation patterns; for example, AI proposes a schedule revision under defined sustainability and safety constraints, supervisors validate and can override with accountability, and the system logs rationale to support auditability and learning.
The closed-loop strategies operationalised as changeable Manufacturing Systems introduces structural uncertainty (quality, timing, and quantity of returned items), and therefore demands both circular logic and reconfigurable operations. Andersen et al. [46] analyse challenges in product take-back and evaluate reconfigurable solutions, highlighting modular and platform-based approaches to handle supply uncertainty for end-of-use items. The key contribution here is not only the circular intent, but the explicit coupling between circular flows and Manufacturing System changeability (capacity, routing, and resource configuration). It means the closed-loop capability requires a Manufacturing System that can reconfigure and still maintain economic and operational viability under reverse-flow uncertainty. Operationally, the short-term difficulty is exception handling load (unpredictable routing and quality dispositions), while the structural challenge is planning stability under persistent reverse-flow volatility.
An overarching stream concerns the assessment, roadmap, and governance models that integrate the three I5.0 pillars. Because “sustainable, flexible, and human-centric” is multi-dimensional, coded works target integrated assessment and strategy formation. Caggiano et al. [48] propose a metamodel for designing assessment models to support the transition of production systems toward I5.0, aiming to structure the dimensions needed for comprehensive evaluation. At the strategic level, van Erp et al. [2] propose an I5.0 manufacturing strategy framework combining process and system models (including “fluid” physical and cyber systems) to support sustainable, resilient, and human-centric value creation. These works help convert broad I5.0 aspirations into traceable capability gaps, decision criteria, and staged transition pathways at both the plant and network levels. A practical gap remains that many multi-criteria proposals do not yet converge on a small set of standardised, decision-grade KPIs that are validated across contexts, which limits comparability and slows industrial uptake.
A particular aspect worth mentioning is the emerging “safety and wellbeing by design” digital layers for human-centric resilience. Sbaragli et al. [11] conceptualise the Safe Operator 5.0 digital architecture, combining sensing (for example, proximity and physiological signals) and ML-based evaluation to provide feedback and early warning that connects operational decisions with worker wellbeing and resilience. In parallel, Human Digital Twin (HDT) research is being positioned as a mechanism to represent individual human needs and capabilities inside the system model; for example, Bucci et al. [33] review how HDTs can support human-centric manufacturing in Industry 5.0 settings and outline open challenges and research directions. These strands make the governance issue explicit: Once safety and wellbeing become digitised, questions of consent, explainability, and legitimate use become part of Manufacturing System design, not external compliance.
3.3. Nurturing an Industry 5.0-Aligned Education Paradigm for Manufacturing Systems
This challenge treats skills and education as a binding constraint for I5.0-aligned Manufacturing Systems evolution: Capability is no longer captured by isolated roles; it depends on a portfolio spanning digital and data fluency, circular and sustainability literacy, and human-centred engineering for safe, trustworthy adoption of advanced automation and AI in operational decision loops. The coded corpus therefore emphasises competence frameworks, scalable delivery mechanisms (for example, micro-credentials), and experiential infrastructures (for example learning factories) as ecosystem levers to sustain continuous upskilling and reskilling (Figure 4). Operationally, this is not only a training problem; it is a performance problem, because insufficient competence shows up as degraded decision quality (for example, misuse of AI recommendations), higher instability under high mix, and slower recovery from disruptions.
Figure 4.
I5.0 skills and education ecosystem for Manufacturing Systems: stakeholder co-creation (industry, academia, policy/intermediaries), learning mechanisms (micro-credentials, learning factories, workplace learning), and the core competence domains required for continuous reskilling and human-centric technology adoption.
Four streams were identified with works that contribute to overcoming this challenge. A first stream proposes structured competence frameworks and taxonomies that help translate the I5.0 pillars into teachable and assessable skill sets. Oeij et al. [57] provide a conceptual framing of workforce skills for I5.0 that is explicitly multi-level and socio-technical, which is helpful to avoid purely “technology-skills checklists”. Complementarily, Carminati et al. [56] derive an integrative skills framework via systematic review and a European survey, highlighting clusters that combine sustainability-related competences with adaptability and leadership, which is particularly relevant for Manufacturing System leaders responsible for twin transition roadmaps. At an ecosystem implementation level, EIT Manufacturing (one of the nine Knowledge and Innovation Communities supported by the European Institute of Innovation and Technology) formalises a competency framework and quality system oriented to skill agility and reducing skill gaps in the European manufacturing sector, which is useful as an operational reference when aligning curricula with industrial upskilling pathways [73]. Short-term barriers here are curricular availability and time-to-train, whereas structural challenges include capability retention, career pathways, and aligning incentives across firms, education providers, and regional intermediaries.
A second stream addresses delivery formats that can scale lifelong learning, notably micro-credentials and modular certification pathways. Walsh Shanahan and Organ [74] discuss micro-credentials as a mechanism connecting learners, higher education institutions, and employers, directly matching the “triple-helix” nature of the education challenge in I5.0. Related work proposes decision support for company-level professional development programme design and selection, reinforcing the need for training portfolios that are adaptive to fast technology and policy shifts [59]. In parallel, manufacturing-focused perspectives underline the strategic role of continuous upskilling and reskilling for advanced manufacturing ecosystems, and the need to treat skills as a resilience mechanism rather than a compliance activity [61]. For SMEs, scalability is decisive: Modular, stackable training reduces opportunity cost, while shared regional offerings reduce the fixed cost of capability building.
A third stream focuses on transforming engineering education itself to match I5.0’s socio-technical demands. Broo et al. [60] argue for rethinking engineering education in the I 5.0 context, moving beyond narrow digitalisation narratives toward broader human-centric and sustainability competences. Complementary education research points to project-based and community-engaged learning as mechanisms to embed sustainability and societal value creation into engineering formation, strengthening the “planet and society” dimension with practice-based evidence [75,76]. This stream is relevant for Manufacturing Systems because it supports competence profiles that can navigate trade-offs (productivity, sustainability, resilience, and human-centricity) rather than optimising a single metric.
Finally, a fourth stream provides experiential infrastructures such as learning and teaching factories adapted to I5.0 requirements. A recent “Learning Factory 5.0” design model explicitly targets human-centric, sustainable, and flexible technical education, positioning open and collaborative principles as enablers for broader adoption [77]. In the same vein, empirical work evaluates training interventions and maps emerging competences for I5.0, which supports more evidence-based training design and assessment rather than relying on generic “future skills” claims [58]. To strengthen decision-grade adoption, future studies should evaluate training interventions against Manufacturing System trajectories (for example, sustained OEE stability under high mix, time-to-recovery after disruptions, energy intensity per unit, and error rates in human–AI decision loops), preferably in longitudinal and cross-site designs.
Despite these advances, there is still limited cumulative evidence connecting (a) specific I5.0 competence-development mechanisms (micro-credentials, learning factories, workplace learning) to (b) measurable Manufacturing System outcomes (for example, circular performance, resilience under disruption, or sustained human-in-the-loop decision quality). This motivates more longitudinal and cross-site research designs where training is evaluated against Manufacturing System performance trajectories, not only learner satisfaction or short-term skill tests.
3.4. Integrative Industrial Scenario and Cross-Cutting Implications
To make the three challenge streams operationally concrete, consider a high-mix manufacturing plant producing configurable products that must comply with emerging lifecycle transparency and circularity expectations. Stream 3.1 introduces DPP-enabled product identity and lifecycle records, which become decision inputs at multiple points: production planning (variant configuration and routing), quality (disposition rules based on certified materials/condition), service (eligibility for upgrade/repair), and end-of-life routing (repair, remanufacture, harvest, recycle). Stream 3.2 then determines whether the plant can absorb the resulting volatility (mix changes, returns uncertainty) through reconfigurability and resilient orchestration, while maintaining sustainability constraints (energy, waste) and human-centric constraints (safe work and accountable decision support). Stream 3.3 becomes the pacing constraint that determines whether supervisors, engineers, and operators can execute these new decision loops reliably, including the ability to interpret passport data, validate AI recommendations, and sustain continuous improvement of multi-criteria performance (Figure 5).
Figure 5.
Dynamic coupling between lifecycle data, operational orchestration, and skills development across Streams 3.1–3.3, showing decision inputs and feedback loops for I5.0-aligned Manufacturing Systems.
In this scenario, short-term implementation barriers typically appear as data readiness and integration load (passport completeness, interoperability across IT/OT, governance of access rights), changeover and scheduling instability under higher variety, and skills gaps in managing human–AI decision workflows. Longer-term structural challenges include standardised, auditable KPI systems for multi-criteria trade-offs, governance at the system-of-systems scale (who is accountable for data quality and decisions across actors), and cumulative evidence that the combined intervention improves both circular outcomes and competitive performance rather than shifting burden elsewhere.
A minimal “decision-grade” KPI set for such deployments can be framed as (i) sustainability: energy intensity per unit, scrap/rework rate, circular routing yield (share repaired/remanufactured vs. recycled), (ii) resilience: time-to-recovery after disruptions, schedule stability under high mix, reverse-flow volatility absorption (WIP amplification), (iii) human-centricity: ergonomic risk index and safety events, workload stability, override frequency and explainability acceptance in human–AI decision loops. Embedding these metrics into planning and control, and validating them longitudinally, is a necessary condition for the research agenda developed in Section 4 to move from plausible architectures to cumulative evidence.
4. Discussion, Research Agenda, and Limitations
I5.0 reframes industrial transformation by treating sustainability, resilience, and human-centricity as system-level objectives, with digitalisation operating primarily as an enabling layer rather than the end goal. The contribution of this study is to translate that normative framing into a traceable Manufacturing Systems lens, using a challenge-centred coded corpus and an evidence-density mapping logic. Section 2 consolidates the post-2020 discourse into four coherent challenge clusters (planet and society, products and consumption, production, people), and Section 3 operationalises that landscape into three Manufacturing Systems’ challenge streams. Read together, the analysis presented suggests that I5.0 is best interpreted as a set of coupled constraints that reshape Manufacturing System design choices, not as an incremental portfolio of “next-generation” technologies. To strengthen external grounding of the resulting research directions, the agenda below was triangulated with insights repeatedly consolidated in systematic literature reviews on (i) Industry 5.0 (human-centric manufacturing, enabling technologies, and implementation challenges) and (ii) Industry 4.0 in manufacturing (sustainability pathways, social implications, and operational trade-offs) [4,78,79,80,81,82]. This triangulation is used to corroborate the priority themes against established syntheses and to keep the proposed research directions focused on under-resolved, decision-relevant gaps, while maintaining the paper’s positioning as a challenge-centred evidence-mapping research contribution.
The synthesis indicates an uneven but coherent solution space across the three Manufacturing System challenge streams. For personalised and circular products (Section 3.1), the dominant response is the construction of lifecycle information infrastructures, especially DPP and related passport or digital-thread concepts. These contributions converge on product identity, traceability, and stakeholder-specific access as prerequisites for making circularity operational at scale. For sustainable, flexible, and human-centric Manufacturing Systems (Section 3.2), the literature converges on architectural responses that combine reconfigurability, decentralised or autonomous orchestration, and explicit human-in-the-loop patterns, supported by emerging assessment metamodels and wellbeing-by-design digital layers. For the education and skills ecosystem (Section 3.3), the evidence base emphasises competence frameworks and scalable delivery mechanisms, such as micro-credentials and learning factories, framing capability development as a multi-actor and continuous reskilling problem rather than a training add-on. At the same time, much of the current contribution base remains conceptual or architecture-level, and comparatively fewer studies deliver decision-grade, multi-criteria validation under real operational constraints (for example, quantified trade-offs, longitudinal outcomes, cross-site robustness). This is consistent with several systematic literature reviews that suggest the key limitation of the current knowledge base is less the absence of proposed concepts and more the scarcity of decision-grade validation (multi-criteria KPIs, governance boundaries, and longitudinal/cross-site evidence) for integrated socio-technical operating models [78,79,81].
Across the literature review publications, several themes recur and align directly with the three streams developed in Section 3. First, I5.0 related ones converge on human-centricity and socio-technical design as differentiators, but emphasise unresolved implementation issues such as governance, ethics, data privacy, and the need for validated human-centric metrics (e.g., [78,79]). Second, Industry 4.0 related ones show that digitalisation can enable resource efficiency and transparency, yet also introduces trade-offs (energy/data burden, rebound effects, and social implications), reinforcing the need for multi-criteria orchestration and auditable measurement (e.g., [4,81,82]). Third, recent I5.0 and sustainability literature reviews highlight the maturity gap between technology roadmaps and operational deployment pathways, particularly in SME contexts and multi-actor ecosystems (e.g., [80]).
Figure 6 crosses the I5.0 components with the three Manufacturing System challenges, clarifying where sustainability, resilience, and human-centricity pressures are reflected in current solution proposals, and where digitalisation is mainly invoked as the backbone that enables traceability, orchestration, and human augmentation.
Figure 6.
Cross-mapping of I5.0 components (sustainability, resilience, human-centricity, and digitalisation as enabler) against the three Manufacturing Systems’ challenge categories (Section 3.1, Section 3.2 and Section 3.3), summarising the response themes in the coded corpus.
Beyond synthesis, this analysis supports framing the next research wave less as a technology roadmap and more as a Manufacturing Systems research agenda that is explicit about infrastructures, orchestration, people, and the conditions required for cumulative evidence. The agenda that emerges from the corpus can be organised into three priority directions. The first concerns lifecycle information infrastructures that make circularity and transparency implementable (for example, product identity, traceability, and interoperable data models that connect PLM, production, logistics, service, and end-of-life contexts). The second concerns operational orchestration and measurement, where the central requirement is decision-grade mechanisms for balancing multi-criteria performance, namely, productivity together with sustainability, resilience, and human-centric outcomes. The third concerns people and learning, including human–automation symbiosis patterns, safe and trustworthy adoption of AI-enabled decision support, and learning ecosystems that can sustain continuous reskilling at the pace required by the twin transition. These directions are consistent with the “macro” priorities repeatedly articulated in Industry 4.0/5.0 literature reviews, but the present study adds a Manufacturing System-specific traceability: It links each priority to a challenge-explicit evidence map and to the three-stream structure (Section 2 and Section 3), thereby sharpening where research should move from principle/architecture proposals to validated operating models. (e.g., [78,79,81]). Therefore, across all three directions, the recurring bottleneck is not “lack of concepts”; it is lack of validated, implementable operating models that bind information, decisions, and accountability into repeatable routines.
Figure 7 summarises the agenda as a matrix linking the three Manufacturing Systems’ challenge streams to the three priority directions above. Two cross-cutting requirements appear in every intersection. The first is evidence that is decision-grade, including validation of integrated outcomes and causal effects at the system level, rather than isolated demonstrations. The second is governance at the system-of-systems scale, including interoperability, access rights, responsibility for data quality, and mechanisms that make trust and accountability defensible across heterogeneous actors. These cross-cutting requirements also provide a pragmatic “readiness test” for proposed solutions: A contribution is closer to deployment when it specifies governance boundaries (who owns data and decisions), performance boundaries (which KPIs and trade-offs are targeted), and validation boundaries (what constitutes evidence in a given industrial context).
Figure 7.
Research agenda matrix for I5.0 Manufacturing Systems, linking the three Manufacturing Systems’ challenge categories (Section 3.1, Section 3.2 and Section 3.3) to priority research directions in information infrastructures, operational orchestration and metrics, and people and learning, with cross-cutting needs in evidence and governance.
Several gaps remain structural from a Manufacturing Systems viewpoint, and they delimit where research contribution is most needed. Lifecycle transparency concepts, including DPP-like mechanisms, are maturing faster than their integration into routine planning and control, and there is still limited evidence on how lifecycle data changes shop-floor and network decisions under uncertainty (for example, how it affects scheduling, quality loops, maintenance, or service strategies without creating prohibitive data burden). Interoperability is frequently assumed while governance is under-specified, particularly regarding responsibility for data quality, boundary definition, confidentiality, and auditable access across mixed-maturity value chains. Multi-criteria performance remains measurement-limited, since the field calls for combined sustainability, resilience, and human-centric outcomes, yet standardised KPIs and assessment models are not sufficiently validated to support comparability across contexts. Human-centricity is often treated conceptually, while fewer studies quantify trade-offs among productivity, safety, workload, trust, and accountability when AI-enabled decision support is embedded in operational routines. Finally, the education and skills stream is expanding rapidly, but evidence linking specific reskilling mechanisms to sustained Manufacturing System performance trajectories remains scarce, which limits guidance on what works, for whom, and under which organisational conditions. To make the implementation challenge more explicit, many short-term barriers are informational and organisational (data readiness, integration effort, skill gaps, and change capacity), whereas the structural challenges are governance- and validation-related (system boundaries, accountability across actors, standardised multi-criteria KPI sets, and longitudinal evidence of net benefit).
This study has limitations that should temper interpretation. The corpus is challenge-centred and selective (n = 30), prioritising sources that articulate explicit barriers, tensions, or capability gaps, which improves traceability but can under-represent adjacent empirical work that addresses similar issues without the I5.0 label. The mapping and coding logic is multi-tag and interpretive, so boundaries between challenge clusters and Manufacturing System pillars are not always sharp, even when applied consistently. The synthesis is non-meta-analytic, and it does not estimate effect sizes or compare interventions quantitatively, since the evidence base is heterogeneous and still includes a substantial conceptual component. I5.0 policy instruments and standards are also evolving, so parts of the agenda, particularly around DPP implementation and governance, should be revisited as delegated acts, data-space initiatives, and sector-specific practices mature. Because coding is performed by a single author, no inter-coder reliability statistics are reported; transparency is therefore supported through an explicit coding rule, a publicly visible coding table (Appendix A, Table A1), and the fact that each source may be traced to multiple map cells. Finally, because this study is not a protocol-driven systematic review, it does not claim comprehensive coverage of all Industry 4.0/5.0 manufacturing publications; the added systematic literature review triangulation is used specifically to ground and cross-check the research agenda and does not substitute for the challenge-centred inclusion rule applied to the coded corpus.
5. Conclusions
This paper translates the post-2020 I5.0 discourse into a Manufacturing System lens that is both traceable to the I5.0 framing and actionable for operations and engineering research. By clustering I5.0 pressures into a compact challenge map (RQ1) and mapping the resulting coded corpus (n = 30) to Manufacturing Systems concerns (RQ2), the analysis makes visible where challenge-explicit contributions concentrate and where they remain fragmented or conceptually stated. The subsequent synthesis consolidates contributions into three Manufacturing Systems challenge streams, clarifying the dominant solution directions currently pursued across information infrastructures, operational orchestration concepts, and people-related capability mechanisms (RQ3).
The resulting contribution is a coherent structure that can be used to position future research, support comparability of contributions, and guide practice-oriented diagnosis of capability gaps when pursuing I5.0-aligned transformation. For industrial practice, the framework supports structured questioning around (i) product and lifecycle data continuity (e.g., DPP-enabled traceability), (ii) multi-criteria orchestration under volatility (sustainability, resilience, and human-centricity together with competitiveness constraints), and (iii) competence-development mechanisms needed to sustain human-in-the-loop decision-making and safe adoption of digital support. The implications in terms of research agenda, structural gaps, and study limitations are discussed in Section 4, which is intended to serve as the primary locus for forward-looking guidance rather than duplicating that content here.
This study has limitations that should temper interpretation. The corpus is challenge-centred and selective, inclusion depended on explicit challenge or barrier statements, and the resulting evidence-density map represents where challenge-explicit contributions occur, not the quality or causal validity of evidence. Coding is multi-tag and interpretive, and no inter-coder reliability statistics are reported, so transparency is supported via the explicit coding rule and Appendix A, Table A1. Future work should prioritise decision-grade empirical validation of the proposed streams (including longitudinal and cross-site studies), the development and testing of I5.0 readiness metrics and multi-criteria KPI sets, and sector- or context-specific studies (including SME feasibility constraints) that quantify trade-offs and implementation barriers such as data governance, integration effort, and skills capacity.
Funding
The author acknowledges Fundação para a Ciência e a Tecnologia (FCT) for its financial support via LAETA (project https://doi.org/10.54499/UID/50022/2025). This work has been supported by the European Union under the Next Generation EU, through a grant of the Portuguese Republic’s Recovery and Resilience Plan (PRR) Partnership Agreement, within the scope of the project PRODUTECH R3—“Agenda Mobilizadora da Fileira das Tecnologias de Produção para a Reindustrialização”, Total project investment: 166.988.013,71 Euros; Total Grant: 97.111.730,27 Euros.
Institutional Review Board Statement
Not applicable.
Informed Consent Statement
Not applicable.
Data Availability Statement
The original contributions presented in this study are included in the article. Further inquiries can be directed to the author.
Conflicts of Interest
The author declares no conflicts of interest.
Abbreviations
The following abbreviations are used in this manuscript:
| AAS | Asset Administration Shell |
| AI | Artificial Intelligence |
| DAM | Decentralised Autonomous Manufacturing |
| DPP | Digital Product Passport |
| DT | Digital Twin |
| HDT | Human Digital Twin |
| I4.0 | Industry 4.0 |
| I5.0 | Industry 5.0 |
| IIoT | Industrial Internet-of-Things |
| IPCC | Intergovernmental Panel on Climate Change |
| KPI | Key Performance Indicator |
| PLM | Product Lifecycle Management |
| SME | Small- and Medium-sized Enterprise |
| UN | United Nations |
Appendix A
Table A1.
Challenge-related corpus (n = 30) of Section 2 and coding. Challenge clusters: PS = planet and society, PC = products and consumption, PR = production, PE = people. Manufacturing System pillars: MP = materials and processes, PTA = product, tooling, assembly, MSO = Manufacturing Systems and operations, COMP = competitiveness and people.
References
- Breque, M.; De Nul, L.; Petridis, A. Industry 5.0: Towards a Sustainable, Human-Centric and Resilient European Industry. European Commission, Publications Office, Directorate-General for Research and Innovation, 2021. Available online: https://data.europa.eu/doi/10.2777/308407 (accessed on 16 February 2026).
- van Erp, T.; Carvalho, N.G.P.; Gerolamo, M.C.; Gonçalves, R.; Rytter, N.G.M.; Gladysz, B. Industry 5.0: A new strategy framework for sustainability management and beyond. J. Clean. Prod. 2024, 461, 142271. [Google Scholar] [CrossRef] [Scilit]
- Piccarozzi, M.; Silvestri, L.; Silvestri, C.; Ruggieri, A. Roadmap to Industry 5.0: Enabling technologies, challenges, and opportunities towards a holistic definition in management studies. Technol. Forecast. Soc. Change 2024, 205, 123467. [Google Scholar] [CrossRef] [Scilit]
- Khan, M.I.; Yasmeen, T.; Khan, M.; Hadi, N.U.; Asif, M.; Farooq, M.; Al-Ghamdi, S.G. Integrating industry 4.0 for enhanced sustainability: Pathways and prospects. Sustain. Prod. Consum. 2025, 54, 149–189. [Google Scholar] [CrossRef] [Scilit]
- European Commission. 2030 Digital Compass: The European Way for the Digital Decade (COM(2021) 118 Final). 2021. Available online: https://eur-lex.europa.eu/legal-content/EN/TXT/HTML/?uri=CELEX:52021DC0118 (accessed on 17 February 2026).
- European Commission. A new Circular Economy Action Plan: For a Cleaner and More Competitive Europe (COM(2020) 98 Final). 2020. Available online: https://eur-lex.europa.eu/legal-content/EN/TXT/HTML/?uri=CELEX:52020DC0098 (accessed on 17 February 2026).
- Xu, X.; Lu, Y.; Vogel-Heuser, B.; Wang, L. Industry 4.0 and Industry 5.0—Inception, conception and perception. J. Manuf. Syst. 2021, 61, 530–535. [Google Scholar] [CrossRef] [Scilit]
- Lu, Y.; Zheng, H.; Chand, S.; Xia, W.; Liu, Z.; Xu, X.; Wang, L.; Qin, Z.; Bao, J. Outlook on human-centric manufacturing towards Industry 5.0. J. Manuf. Syst. 2022, 62, 612–627. [Google Scholar] [CrossRef] [Scilit]
- Ghobakhloo, M.; Iranmanesh, M.; Foroughi, B.; Tirkolaee, E.B.; Asadi, S.; Amran, A. Industry 5.0 implications for inclusive sustainable manufacturing: An evidence-knowledge-based strategic roadmap. J. Clean. Prod. 2023, 417, 138023. [Google Scholar] [CrossRef] [Scilit]
- Peruzzini, M.; Prati, E.; Pellicciari, M. A framework to design smart manufacturing systems for Industry 5.0 based on the human-automation symbiosis. Int. J. Comput. Integr. Manuf. 2024, 37, 1426–1443. [Google Scholar] [CrossRef] [Scilit]
- Sbaragli, A.; Tomelleri, F.; Picariello, F.; Picariello, E.; Pilati, F. Safe Operator 5.0 digital architecture: Towards resilient human-centric manufacturing systems. IFAC-PapersOnLine 2024, 58, 265–270. [Google Scholar] [CrossRef] [Scilit]
- Wang, M.; Tong, Y.; Zhuang, C.; Du, X. Towards industry 5.0: A framework of reconfigurable matrix-structured manufacturing system. J. Manuf. Syst. 2025, 82, 114–136. [Google Scholar] [CrossRef] [Scilit]
- ElMaraghy, H.; Monostori, L.; Schuh, G.; ElMaraghy, W. Evolution and future of manufacturing systems. CIRP Ann. 2021, 70, 635–658. [Google Scholar] [CrossRef] [Scilit]
- Koren, Y. The Global Manufacturing Revolution: Product-Process-Business Integration and Reconfigurable Systems; John Wiley & Sons, Inc.: Hoboken, NJ, USA, 2010. [Google Scholar] [CrossRef] [Scilit]
- Agote-Garrido, A.; Martín-Gómez, A.M.; Lama-Ruiz, J.R. Manufacturing System Design in Industry 5.0: Incorporating Sociotechnical Systems and Social Metabolism for Human-Centered, Sustainable, and Resilient Production. Systems 2023, 11, 537. [Google Scholar] [CrossRef] [Scilit]
- Mott, R.; Jack, H.; Raju, V.; Stratton, M. The Four Pillars of Manufacturing Engineering. In Annual Conference, Society of Manufacturing Engineering; Society of Manufacturing Engineering: Bellevue, MA, USA, 2011. [Google Scholar]
- European Commission. ERA Industrial Technologies Roadmap on Human-Centric Research and Innovation for the Manufacturing Sector; Publications Office of the European Union: Luxembourg, 2024. [Google Scholar]
- Lopes, C.; Barata, J. Digital Product Passport: A Review and Research Agenda. Procedia Comput. Sci. 2024, 246, 981–990. [Google Scholar] [CrossRef] [Scilit]
- Plociennik, C.; Nazeri, A.; Rimaz, M.H.; Knetsch, S.; Lopes, A.D.C.P.; Hagedorn, T.; Baehr, J.; Vogelgesang, M.; Li, C.; Benner, W.; et al. Connecting Producers and Recyclers: A Digital Product Passport Concept and Implementation Suitable for End-of-Life Management. Procedia CIRP 2024, 122, 831–836. [Google Scholar] [CrossRef] [Scilit]
- Kühn, M.; Baumann, M.; Volz, F.; Stojanovic, L. Digital Product Passport Design Supporting the Circular Economy Based on the Asset Administration Shell. Sustainability 2025, 17, 969. [Google Scholar] [CrossRef] [Scilit]
- Sariişik, G.; Demir, S. Industry 5.0: A human-centric paradigm for sustainable and resilient industrial transformation. J. Soc. Perspect. Stud. 2025, 2, 50–66. [Google Scholar] [CrossRef]
- Maddikunta, P.K.R.; Pham, Q.-V.; Prabadevi, B.; Deepa, N.; Dev, K.; Gadekallu, T.R.; Ruby, R.; Liyanage, M. Industry 5.0: A survey on enabling technologies and potential applications. J. Ind. Inf. Integr. 2022, 26, 100257. [Google Scholar] [CrossRef] [Scilit]
- European Commission. Updating the 2020 New Industrial Strategy: Building a Stronger Single Market for Europe’s Recovery (COM(2021) 350 Final). 2021. Available online: https://ec.europa.eu/commission/presscorner/detail/en/ip_21_1884 (accessed on 17 February 2026).
- IPCC. Climate Change 2023: Synthesis Report. Contribution of Working Groups I, II and III to the Sixth Assessment Report of the Intergovernmental Panel on Climate Change; Core Writing Team, Lee, H., Romero, J., Eds.; IPCC: Geneva, Switzerland, 2023. [Google Scholar] [CrossRef] [Scilit]
- United Nations. Transforming Our World: The 2030 Agenda for Sustainable Development. 2015. Available online: https://sdgs.un.org/2030agenda (accessed on 16 February 2026).
- Hussain, Z.; Mohammad, S.I.; Vasudevan, A.; Awad, A.; Bansal, R. Exploring the effect of industry 5.0 human-centric sustainability and green knowledge automation in enhancing green process adaptability: The mediating role of sustainable human-tech interaction. J. Clean. Prod. 2025, 537, 147240. [Google Scholar] [CrossRef] [Scilit]
- Mehta, K.; Solanki, U.; Pal, S.; Ranjan, R.; Nagasampige, M. Industry 5.0 era enabling the transition of logistics to smart logistics: A bibliometric and systematic review. Asian J. Shipp. Logist. 2026. [Google Scholar] [CrossRef] [Scilit]
- Nayeri, S.; Sazvar, Z.; Tirkolaee, E.B. Industry 5.0-driven circular supply chain network design: A novel multi-stage decision-making method. Renew. Sustain. Energy Rev. 2026, 226, 116420. [Google Scholar] [CrossRef] [Scilit]
- Rejeb, A.; Rejeb, K.; Keogh, J.G.; Süle, E. When Industry 5.0 Meets the Circular Economy: A Systematic Literature Review. Circ. Econ. Sustain. 2025, 5, 2621–2652. [Google Scholar] [CrossRef] [Scilit]
- John, L.; Sampayo, M.; Peças, P. Lean & Green on Industry 4.0 Context—Contribution to Understand L&G Drivers and Design Principles. Int. J. Math. Eng. Manag. Sci. 2021, 6, 1214–1229. [Google Scholar] [CrossRef] [Scilit]
- Geissdoerfer, M.; Vladimirova, D.; Evans, S. Sustainable business model innovation: A review. J. Clean. Prod. 2018, 198, 401–416. [Google Scholar] [CrossRef] [Scilit]
- Bocken, N.; Boons, F.; Baldassarre, B. Sustainable business model experimentation by understanding ecologies of business models. J. Clean. Prod. 2019, 208, 1498–1512. [Google Scholar] [CrossRef] [Scilit]
- Bucci, I.; Fani, V.; Bandinelli, R. Towards Human-Centric Manufacturing: Exploring the Role of Human Digital Twins in Industry 5.0. Sustainability 2024, 17, 129. [Google Scholar] [CrossRef] [Scilit]
- Nahavandi, S. Industry 5.0—A human-centric solution. Sustainability 2019, 11, 4371. [Google Scholar] [CrossRef] [Scilit]
- Turner, C.; Oyekan, J.; Garn, W.; Duggan, C.; Abdou, K. Industry 5.0 and the Circular Economy: Utilizing LCA with Intelligent Products. Sustainability 2022, 14, 14847. [Google Scholar] [CrossRef] [Scilit]
- Paul, M.; Gong, S.Q.-C.; Löffler, J.; Reinhart, G. Enhancing product design for remanufacturing: Guidelines and their implementation in integrated remanufacturing systems. Prod. Manuf. Res. 2024, 12, 2396363. [Google Scholar] [CrossRef] [Scilit]
- Ortner, P.; Tay, J.Z.; Wortmann, T. Computational optimization for circular economy product design. J. Clean. Prod. 2022, 362, 132340. [Google Scholar] [CrossRef] [Scilit]
- Rotondo, B.; Bakker, C.; Balkenende, R.; Arquilla, V. Integrating Circular Economy Principles in the New Product Development Process: A Systematic Literature Review and Classification of Available Circular Design Tools. Sustainability 2025, 17, 4155. [Google Scholar] [CrossRef] [Scilit]
- Zhang, Z.; Gu, J.; Li, R.; Lian, W.; Ma, C.; Tian, J. Bridging digital and green transitions: A literature review of digital product passport systems. Renew. Sustain. Energy Rev. 2026, 228, 116600. [Google Scholar] [CrossRef] [Scilit]
- Psarommatis, F.; Konstantinidis, F.; Azamfirei, V.; May, G. Identification of the benefits from the use of Digital Product Passport in a value chain and single organizations. IFAC-PapersOnLine 2024, 58, 301–306. [Google Scholar] [CrossRef] [Scilit]
- Yuan, L. Digital product passports in the circular economy: A reflexive law approach to policy-actor governance tensions. Law Innov. Technol. 2025, 1–29. [Google Scholar] [CrossRef] [Scilit]
- Touriki, F.E.; Benkhati, I.; Kamble, S.S.; Belhadi, A.; El fezazi, S. An integrated smart, green, resilient, and lean manufacturing framework: A literature review and future research directions. J. Clean. Prod. 2021, 319, 128691. [Google Scholar] [CrossRef] [Scilit]
- Peças, P.; John, L.; Ribeiro, I.; Al, E. Holistic Framework to Data-Driven Sustainability Assessment. Sustainability 2023, 15, 3562. [Google Scholar] [CrossRef] [Scilit]
- Peças, P.; Faustino, M.; Lopes, J.; Amaral, A. Lean methods digitization towards lean 4.0: A case study of e-VMB and e-SMED. Int. J. Interact. Des. Manuf. 2022, 16, 1397–1415. [Google Scholar] [CrossRef] [Scilit]
- Delpla, V.; Kenné, J.P.; Hof, L.A. Circular manufacturing 4.0: Towards internet of things embedded closed-loop supply chains. Int. J. Adv. Manuf. Technol. 2022, 118, 3241–3264. [Google Scholar] [CrossRef] [Scilit]
- Andersen, A.L.; Brunoe, T.D.; Bockholt, M.T.; Napoleone, A.; Kristensen, J.H.; Colli, M.; Wæhrens, B.V.; Nielsen, K. Changeable closed-loop manufacturing systems: Challenges in product take-back and evaluation of reconfigurable solutions. Int. J. Prod. Res. 2023, 61, 839–858. [Google Scholar] [CrossRef] [Scilit]
- Martinho, R.; Lopes, J.; Jorge, D.; de Oliveira, L.C.; Henriques, C.; Peças, P. IoT Based Automatic Diagnosis for Continuous Improvement. Sustainability 2022, 14, 9687. [Google Scholar] [CrossRef] [Scilit]
- Caggiano, M.; Semeraro, C.; Dassisti, M. A Metamodel for Designing Assessment Models to support transition of production systems towards Industry 5.0. Comput. Ind. 2023, 152, 104008. [Google Scholar] [CrossRef] [Scilit]
- Nasir, V.; Hosseini, A.; Binfield, L.; Hasani, N.; Ghotb, S.; Diederichs, V.; O Fox, G.; McCann, A.J.; Riggio, M.; Chandler, K.D.; et al. Human-centric Industry 5.0 manufacturing: A multi-level framework from design to consumption within Society 5.0. Int. J. Sustain. Eng. 2025, 18, 2551000. [Google Scholar] [CrossRef] [Scilit]
- Yang, J.; Liu, Y.; Morgan, P.L. Human–machine interaction towards Industry 5.0: Human-centric smart manufacturing. Digit. Eng. 2024, 2, 100013. [Google Scholar] [CrossRef] [Scilit]
- Wang, L.; Gao, R.X.; Krüger, J.; Váncza, J. Human-centric assembly in smart factories. CIRP Ann. 2025, 74, 789–815. [Google Scholar] [CrossRef] [Scilit]
- Alves, J.; Lima, T.M.; Gaspar, P.D. Is Industry 5.0 a Human-Centred Approach? A Systematic Review. Processes 2023, 11, 193. [Google Scholar] [CrossRef] [Scilit]
- Meftah, S.; Sahnoun, M.; Messaadia, M.; Benslimane, S.-M. Enhancing decision-making in Industry 5.0 through adaptive human–machine interfaces: A systematic literature review. Comput. Stand. Interfaces 2026, 96, 104091. [Google Scholar] [CrossRef] [Scilit]
- Tóth, A.; Nagy, L.; Kennedy, R.; Bohuš, B.; Abonyi, J.; Ruppert, T. The human-centric Industry 5.0 collaboration architecture. MethodsX 2023, 11, 102260. [Google Scholar] [CrossRef] [Scilit]
- Giugliano, G.; Capece, S.; Laudante, E.; Muñoz, V.F.M.; Buono, M. Smart Wearable Devices and Technologies for Human-Augmentation Industry 5.0: A Systematic Review. Appl. Sci. 2026, 16, 1481. [Google Scholar] [CrossRef] [Scilit]
- Carminati, L.; Lagorio, A.; Cimini, C.; Pirola, F.; Jurczuk, A.; Boucher, X. Integrative skills framework for Industry 5.0: Insights from a systematic literature review and a European survey study. J. Environ. Manag. 2025, 394, 127425. [Google Scholar] [CrossRef] [Scilit]
- Oeij, P.; Rhijn, G.; Dijk, W.; Krause, F.; Dickinson, P.; Warhurst, C.; Garmann Johnsen, H.C.; Knudsen, J.P.; Schröder, A.; Kopp, R.; et al. Conceptual Framework of Industry 5.0 to Study Workforce Skills (BRIDGES 5.0 Deliverable D1.1/Version 2). 2023. Available online: https://bridges5-0.eu/publications (accessed on 16 February 2026).
- Papacharalampopoulos, A.; Karagianni, O.M.; Fedeli, M.; Lackner, P.; Aleksandraviciene, G.; Ippolito, M.; Elorza, U.; Schröder, A.J.; Stavropoulos, P. Training for Industry 5.0: Evaluating Effectiveness and Mapping Emerging Competences. Machines 2025, 13, 825. [Google Scholar] [CrossRef] [Scilit]
- Leon, R.D. Employees’ reskilling and upskilling for industry 5.0: Selecting the best professional development programmes. Technol. Soc. 2023, 75, 102393. [Google Scholar] [CrossRef] [Scilit]
- Broo, D.G.; Kaynak, O.; Sait, S.M. Rethinking engineering education at the age of industry 5.0. J. Ind. Inf. Integr. 2022, 25, 100311. [Google Scholar] [CrossRef] [Scilit]
- Gal, H.C.; Cohen, Y. Exploring the Skills Revolution: Strategic Upskilling and Reskilling Human Operators for Advanced Manufacturing Ecosystems. IFAC-PapersOnLine 2025, 59, 239–244. [Google Scholar] [CrossRef] [Scilit]
- Mejía, C.A.; Kang, M.; Shisler, S. Evidence Gap Maps as a Tool for Evidence-Informed Decision-Making; Inter-American Development Bank: Washington, DC, USA, 2025. [Google Scholar] [CrossRef] [Scilit]
- van Capelleveen, G.; Vegter, D.; Olthaar, M.; van Hillegersberg, J. The anatomy of a passport for the circular economy: A conceptual definition, vision and structured literature review. Resour. Conserv. Recycl. Adv. 2023, 17, 200131. [Google Scholar] [CrossRef] [Scilit]
- Leng, J.; Zhong, Y.; Lin, Z.; Xu, K.; Mourtzis, D.; Zhou, X.; Zheng, P.; Liu, Q.; Zhao, J.L.; Shen, W. Towards resilience in Industry 5.0: A decentralized autonomous manufacturing paradigm. J. Manuf. Syst. 2023, 71, 95–114. [Google Scholar] [CrossRef] [Scilit]
- Wicaksono, H.; Mengistu, A.; Bashyal, A.; Fekete, T. Digital Product Passport (DPP) technological advancement and adoption framework: A systematic literature review. Procedia Comput. Sci. 2025, 253, 2980–2989. [Google Scholar] [CrossRef] [Scilit]
- Mulhall, D.; Ayed, A.-C.; Schroeder, J.; Hansen, K.; Wautelet, T. The Product Circularity Data Sheet—A Standardized Digital Fingerprint for Circular Economy Data about Products. Energies 2022, 15, 3397. [Google Scholar] [CrossRef] [Scilit]
- Çetin, S.; Raghu, D.; Honic, M.; Straub, A.; Gruis, V. Data requirements and availabilities for material passports: A digitally enabled framework for improving the circularity of existing buildings. Sustain. Prod. Consum. 2023, 40, 422–437. [Google Scholar] [CrossRef] [Scilit]
- Bianchini, D.; Fapanni, T.; Garda, M.; Leotta, F.; Mecella, M.; Rula, A.; Sardini, E. Digital Thread for Smart Products: A Survey on Technologies, Challenges, and Opportunities in Service-Oriented Supply Chains. IEEE Access 2024, 12, 125284–125305. [Google Scholar] [CrossRef] [Scilit]
- Seegrün, A.; Kruschke, T.; Mügge, J.; Hardinghaus, L.; Knauf, T.; Riedelsheimer, T.; Lindow, K. Sustainable product lifecycle management with Digital Twins: A systematic literature review. Procedia CIRP 2023, 119, 776–781. [Google Scholar] [CrossRef] [Scilit]
- Mügge, J.; Seegrün, A.; Hoyer, T.-K.; Riedelsheimer, T.; Lindow, K. Digital Twins within the Circular Economy: Literature Review and Concept Presentation. Sustainability 2024, 16, 2748. [Google Scholar] [CrossRef] [Scilit]
- Wang, B.; Zheng, P.; Yin, Y.; Shih, A.; Wang, L. Toward human-centric smart manufacturing: A human-cyber-physical systems (HCPS) perspective. J. Manuf. Syst. 2022, 63, 471–490. [Google Scholar] [CrossRef] [Scilit]
- Grosse, E.H.; Sgarbossa, F.; Berlin, C.; Neumann, W.P. Human-centric production and logistics system design and management: Transitioning from Industry 4.0 to Industry 5.0. Int. J. Prod. Res. 2023, 61, 7749–7759. [Google Scholar] [CrossRef] [Scilit]
- EIT Manufacturing. Upskilling and Reskilling Quality System and Competency Framework and Education Programmes (Annex B). 2023. Available online: https://www.eitmanufacturing.eu/wp-content/uploads/2023/09/annex-b.pdf (accessed on 17 February 2026).
- Shanahan, B.W.; Organ, J. Harnessing the Benefits of Micro Credentials for Industry 4.0 and 5.0: Skills Training and Lifelong Learning. IFAC-PapersOnLine 2022, 55, 82–87. [Google Scholar] [CrossRef] [Scilit]
- Goggins, J.; Hajdukiewicz, M. The Role of Community-Engaged Learning in Engineering Education for Sustainable Development. Sustainability 2022, 14, 8208. [Google Scholar] [CrossRef] [Scilit]
- Lantada, A.D. Engineering Education 5.0: Strategies for a Successful Transformative Project-Based Learning. In Insights Into Global Engineering Education After the Birth of Industry 5.0; Bouezzeddine, M., Ed.; IntechOpen: London, UK, 2022; pp. 1–17. [Google Scholar] [CrossRef] [Scilit]
- Amaral, A.; Peças, P. SMEs and Industry 4.0: Two case studies of digitalization for a smoother integration. Comput. Ind. 2020, 125, 103333. [Google Scholar] [CrossRef] [Scilit]
- Ghobakhloo, M.; Iranmanesh, M.; Tseng, M.-L.; Grybauskas, A.; Stefanini, A.; Amran, A. Behind the definition of Industry 5.0: A systematic review of technologies, principles, components, and values. J. Ind. Prod. Eng. 2023, 40, 432–447. [Google Scholar] [CrossRef] [Scilit]
- Valette, E.; El-Haouzi, H.B.; Demesure, G. Industry 5.0 and its technologies: A systematic literature review upon the human place into IoT- and CPS-based industrial systems. Comput. Ind. Eng. 2023, 184, 109426. [Google Scholar] [CrossRef] [Scilit]
- Narkhede, G.B.; Pasi, B.N.; Rajhans, N.; Kulkarni, A. Industry 5.0 and sustainable manufacturing: A systematic literature review. Benchmarking Int. J. 2025, 32, 608–635. [Google Scholar] [CrossRef] [Scilit]
- Ching, N.T.; Ghobakhloo, M.; Iranmanesh, M.; Maroufkhani, P.; Asadi, S. Industry 4.0 applications for sustainable manufacturing: A systematic literature review and a roadmap to sustainable development. J. Clean. Prod. 2022, 334, 130133. [Google Scholar] [CrossRef] [Scilit]
- Grybauskas, A.; Stefanini, A.; Ghobakhloo, M. Social sustainability in the age of digitalization: A systematic literature Review on the social implications of industry 4.0. Technol. Soc. 2022, 70, 101997. [Google Scholar] [CrossRef] [Scilit]
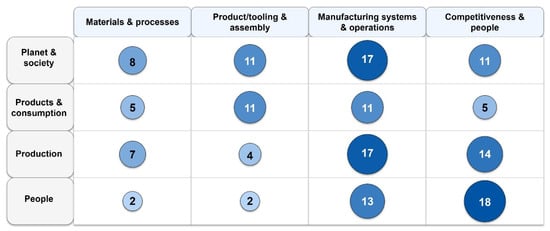
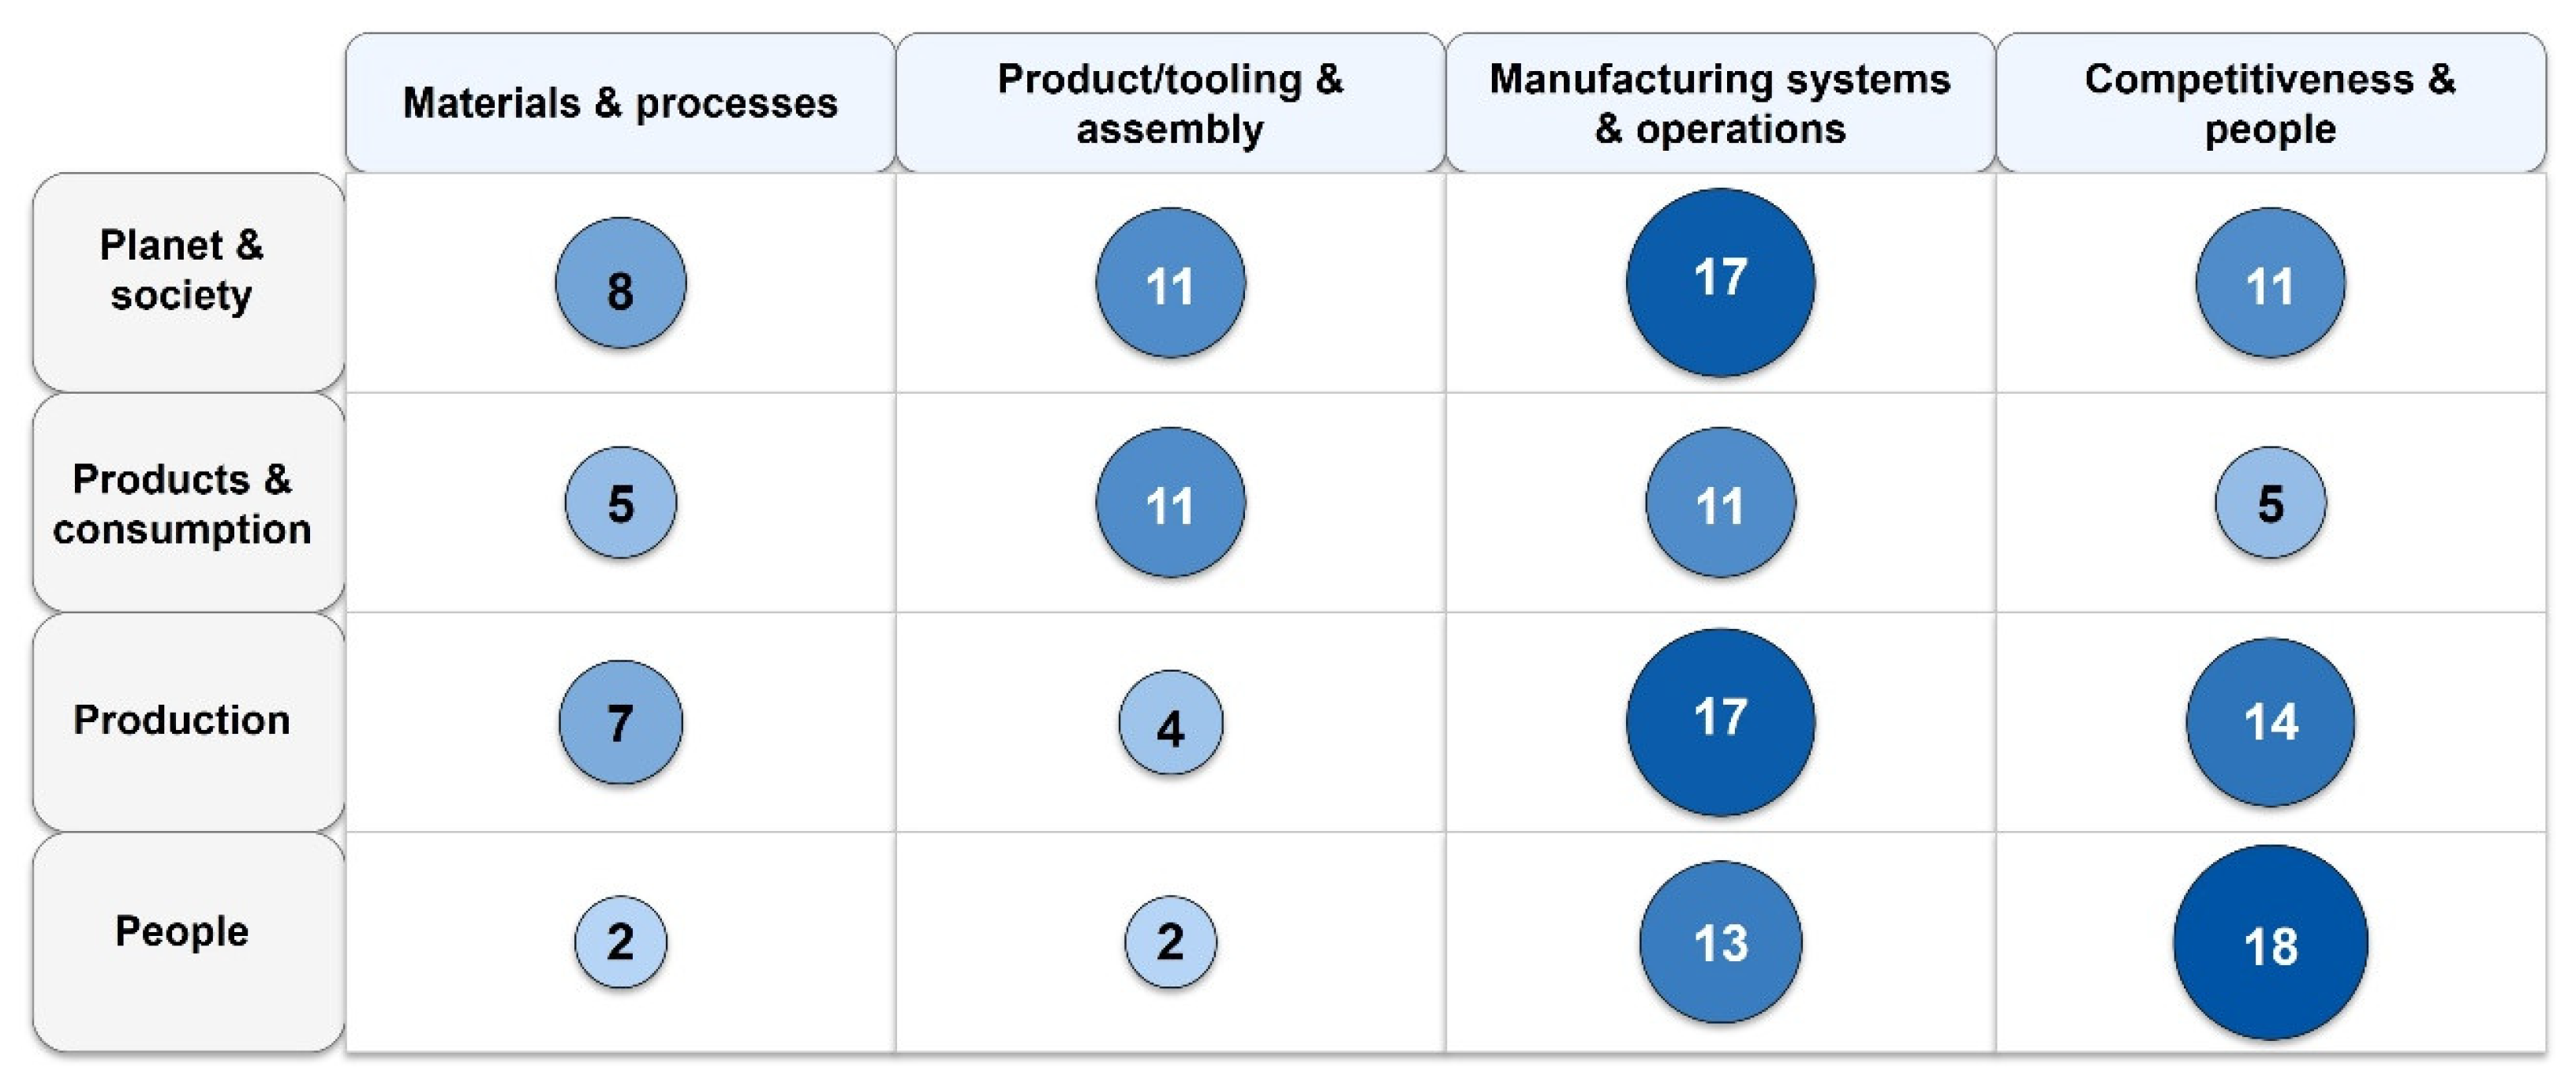
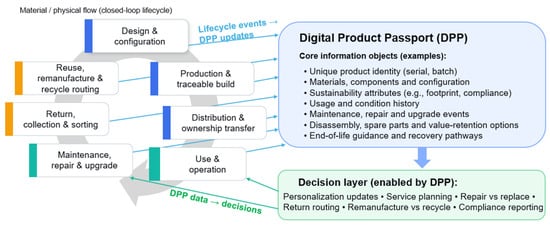
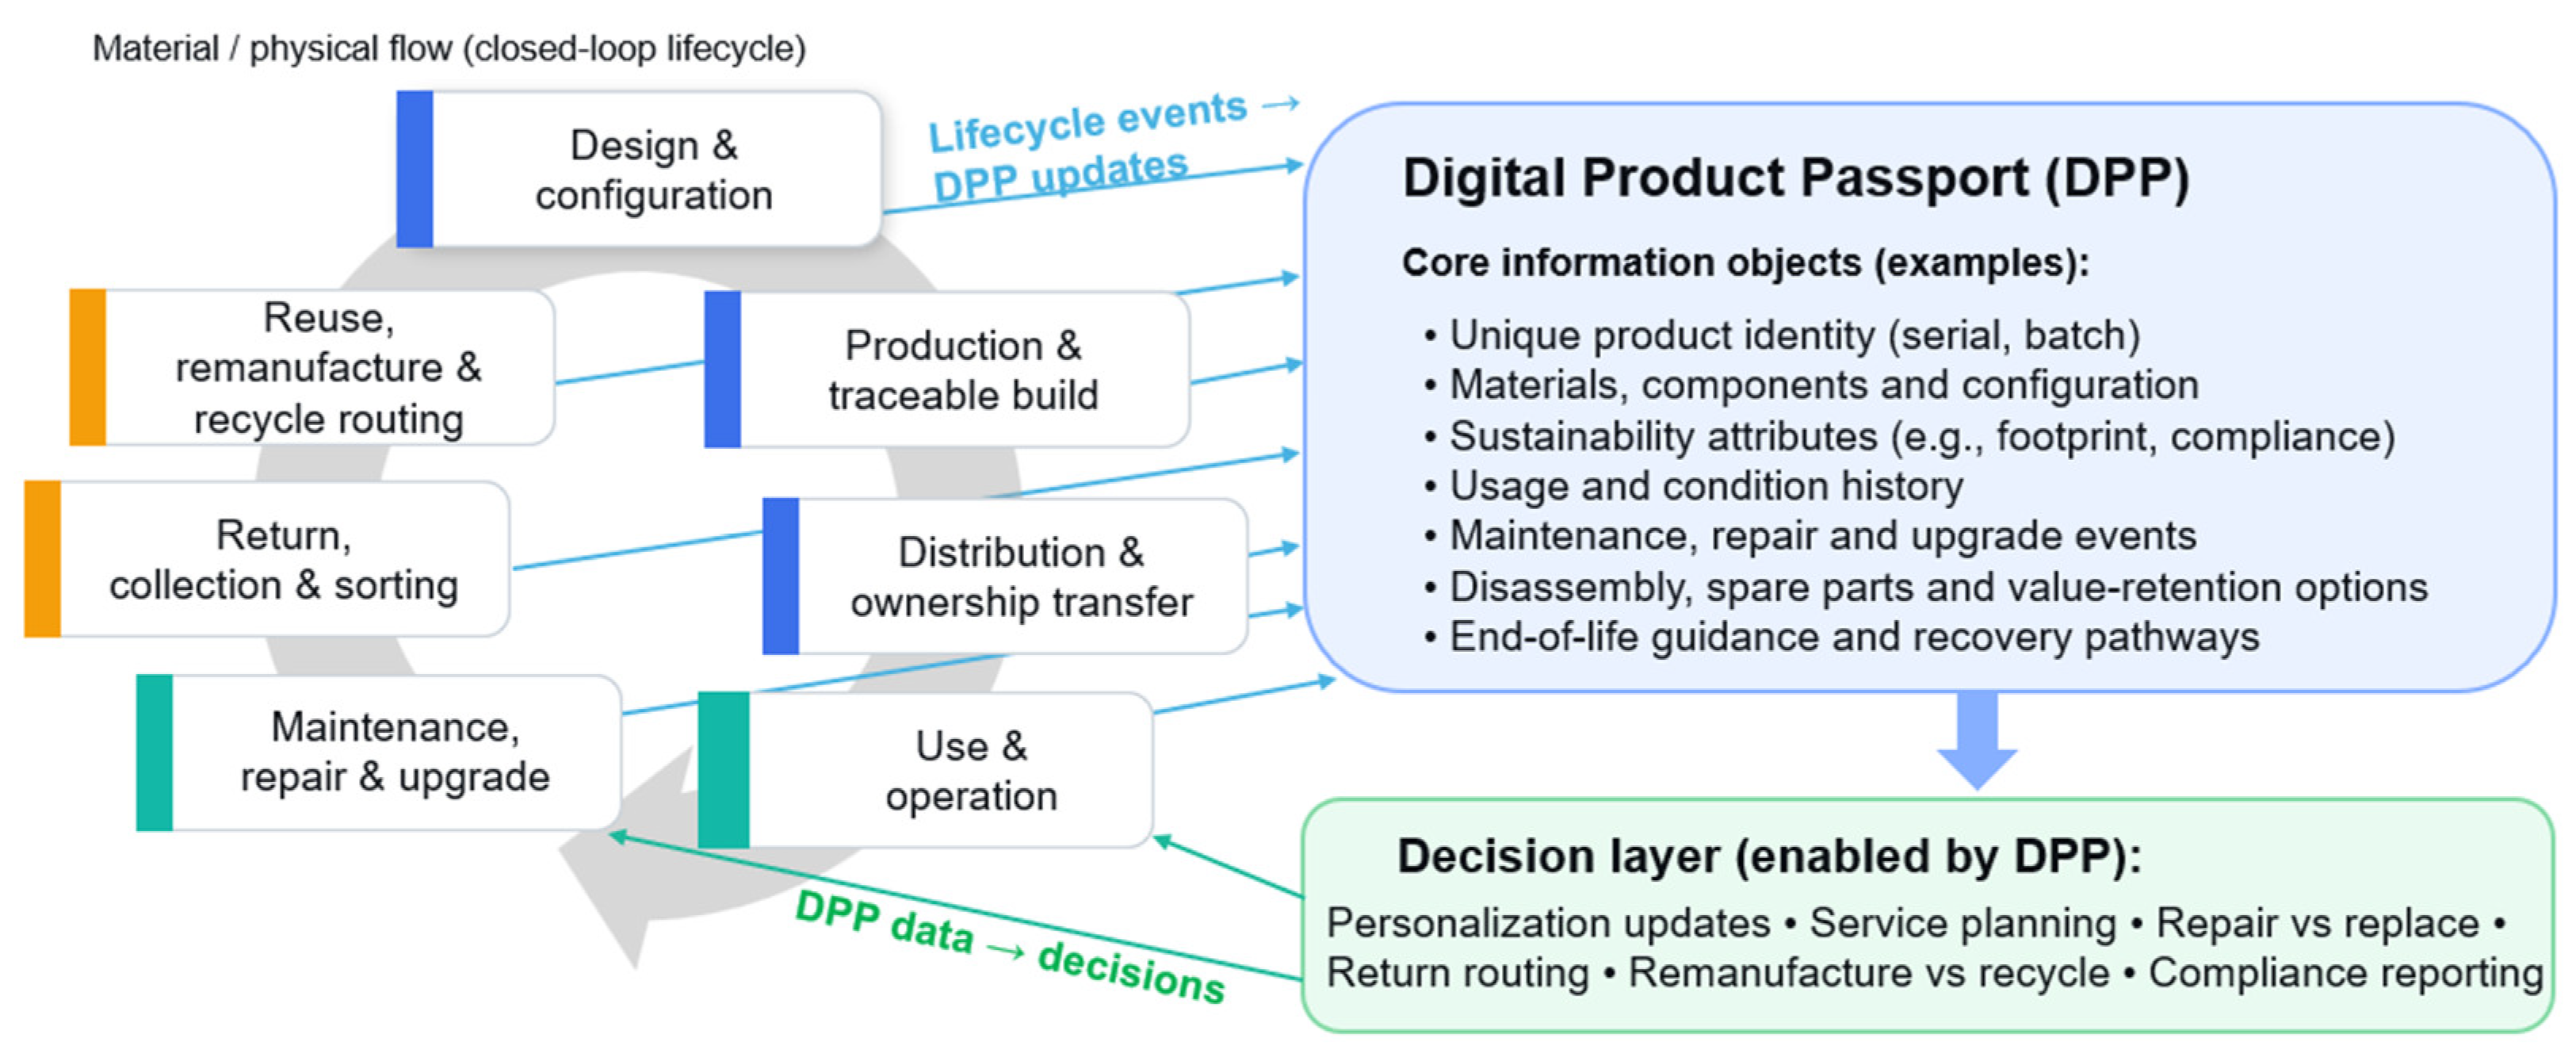
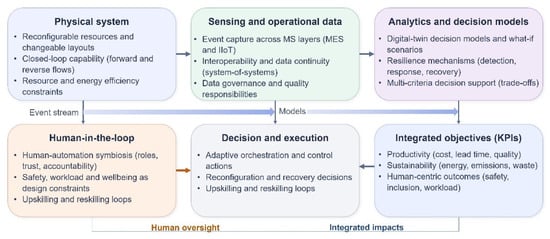
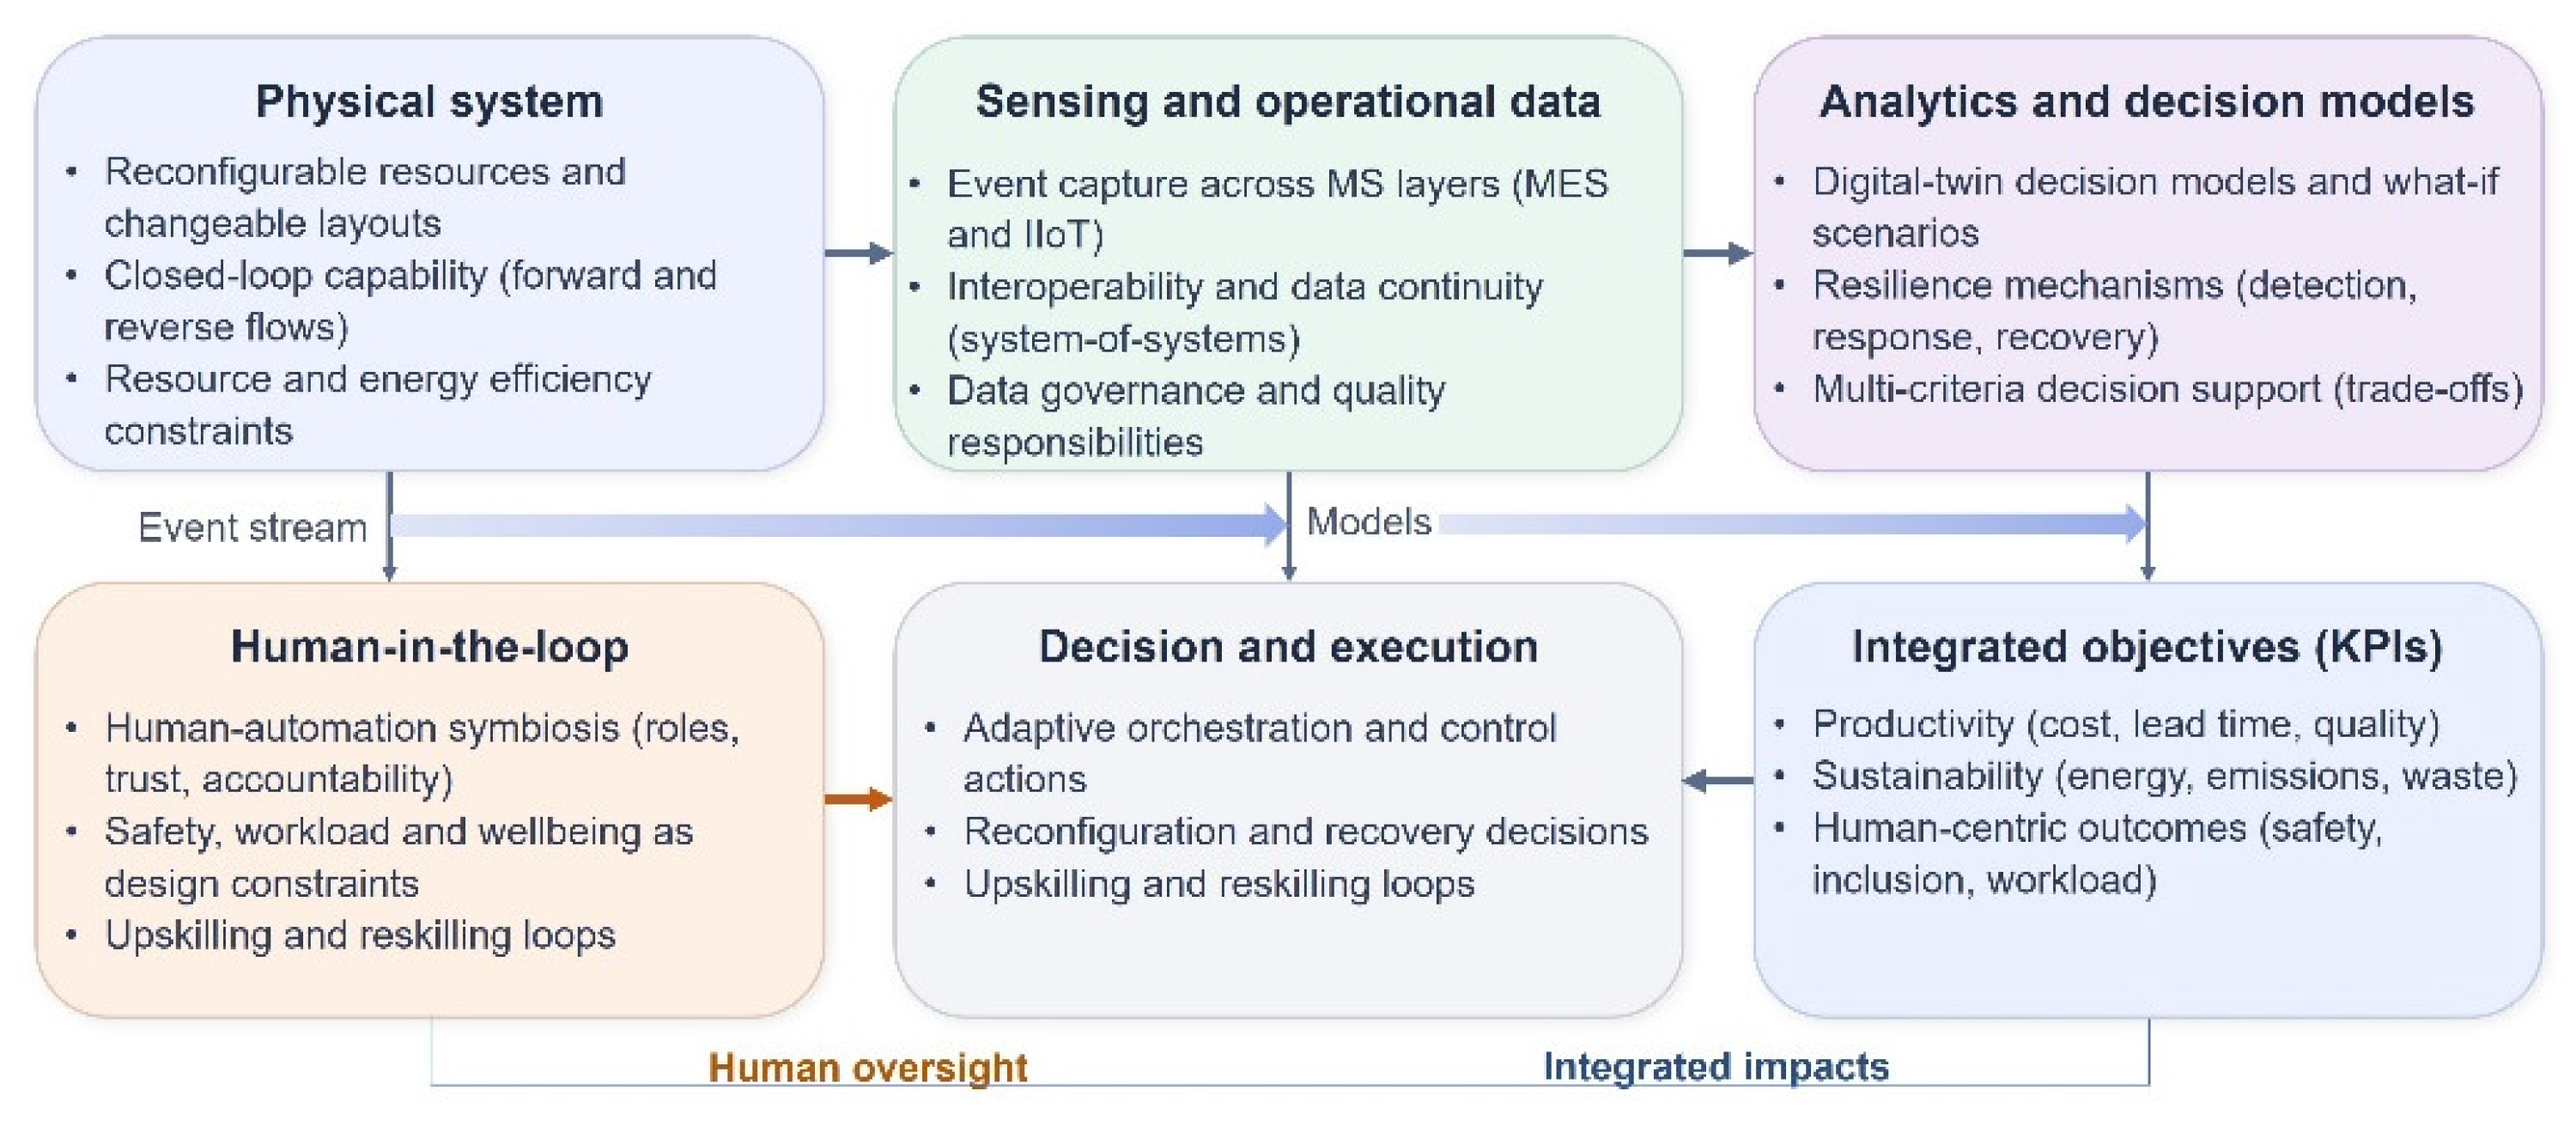
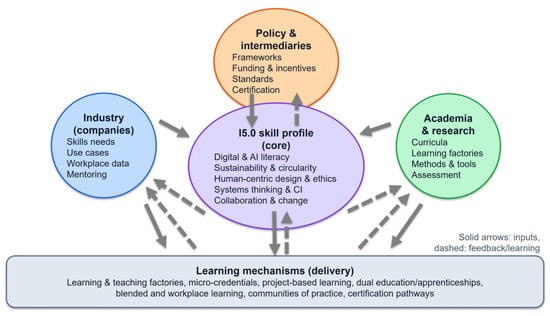
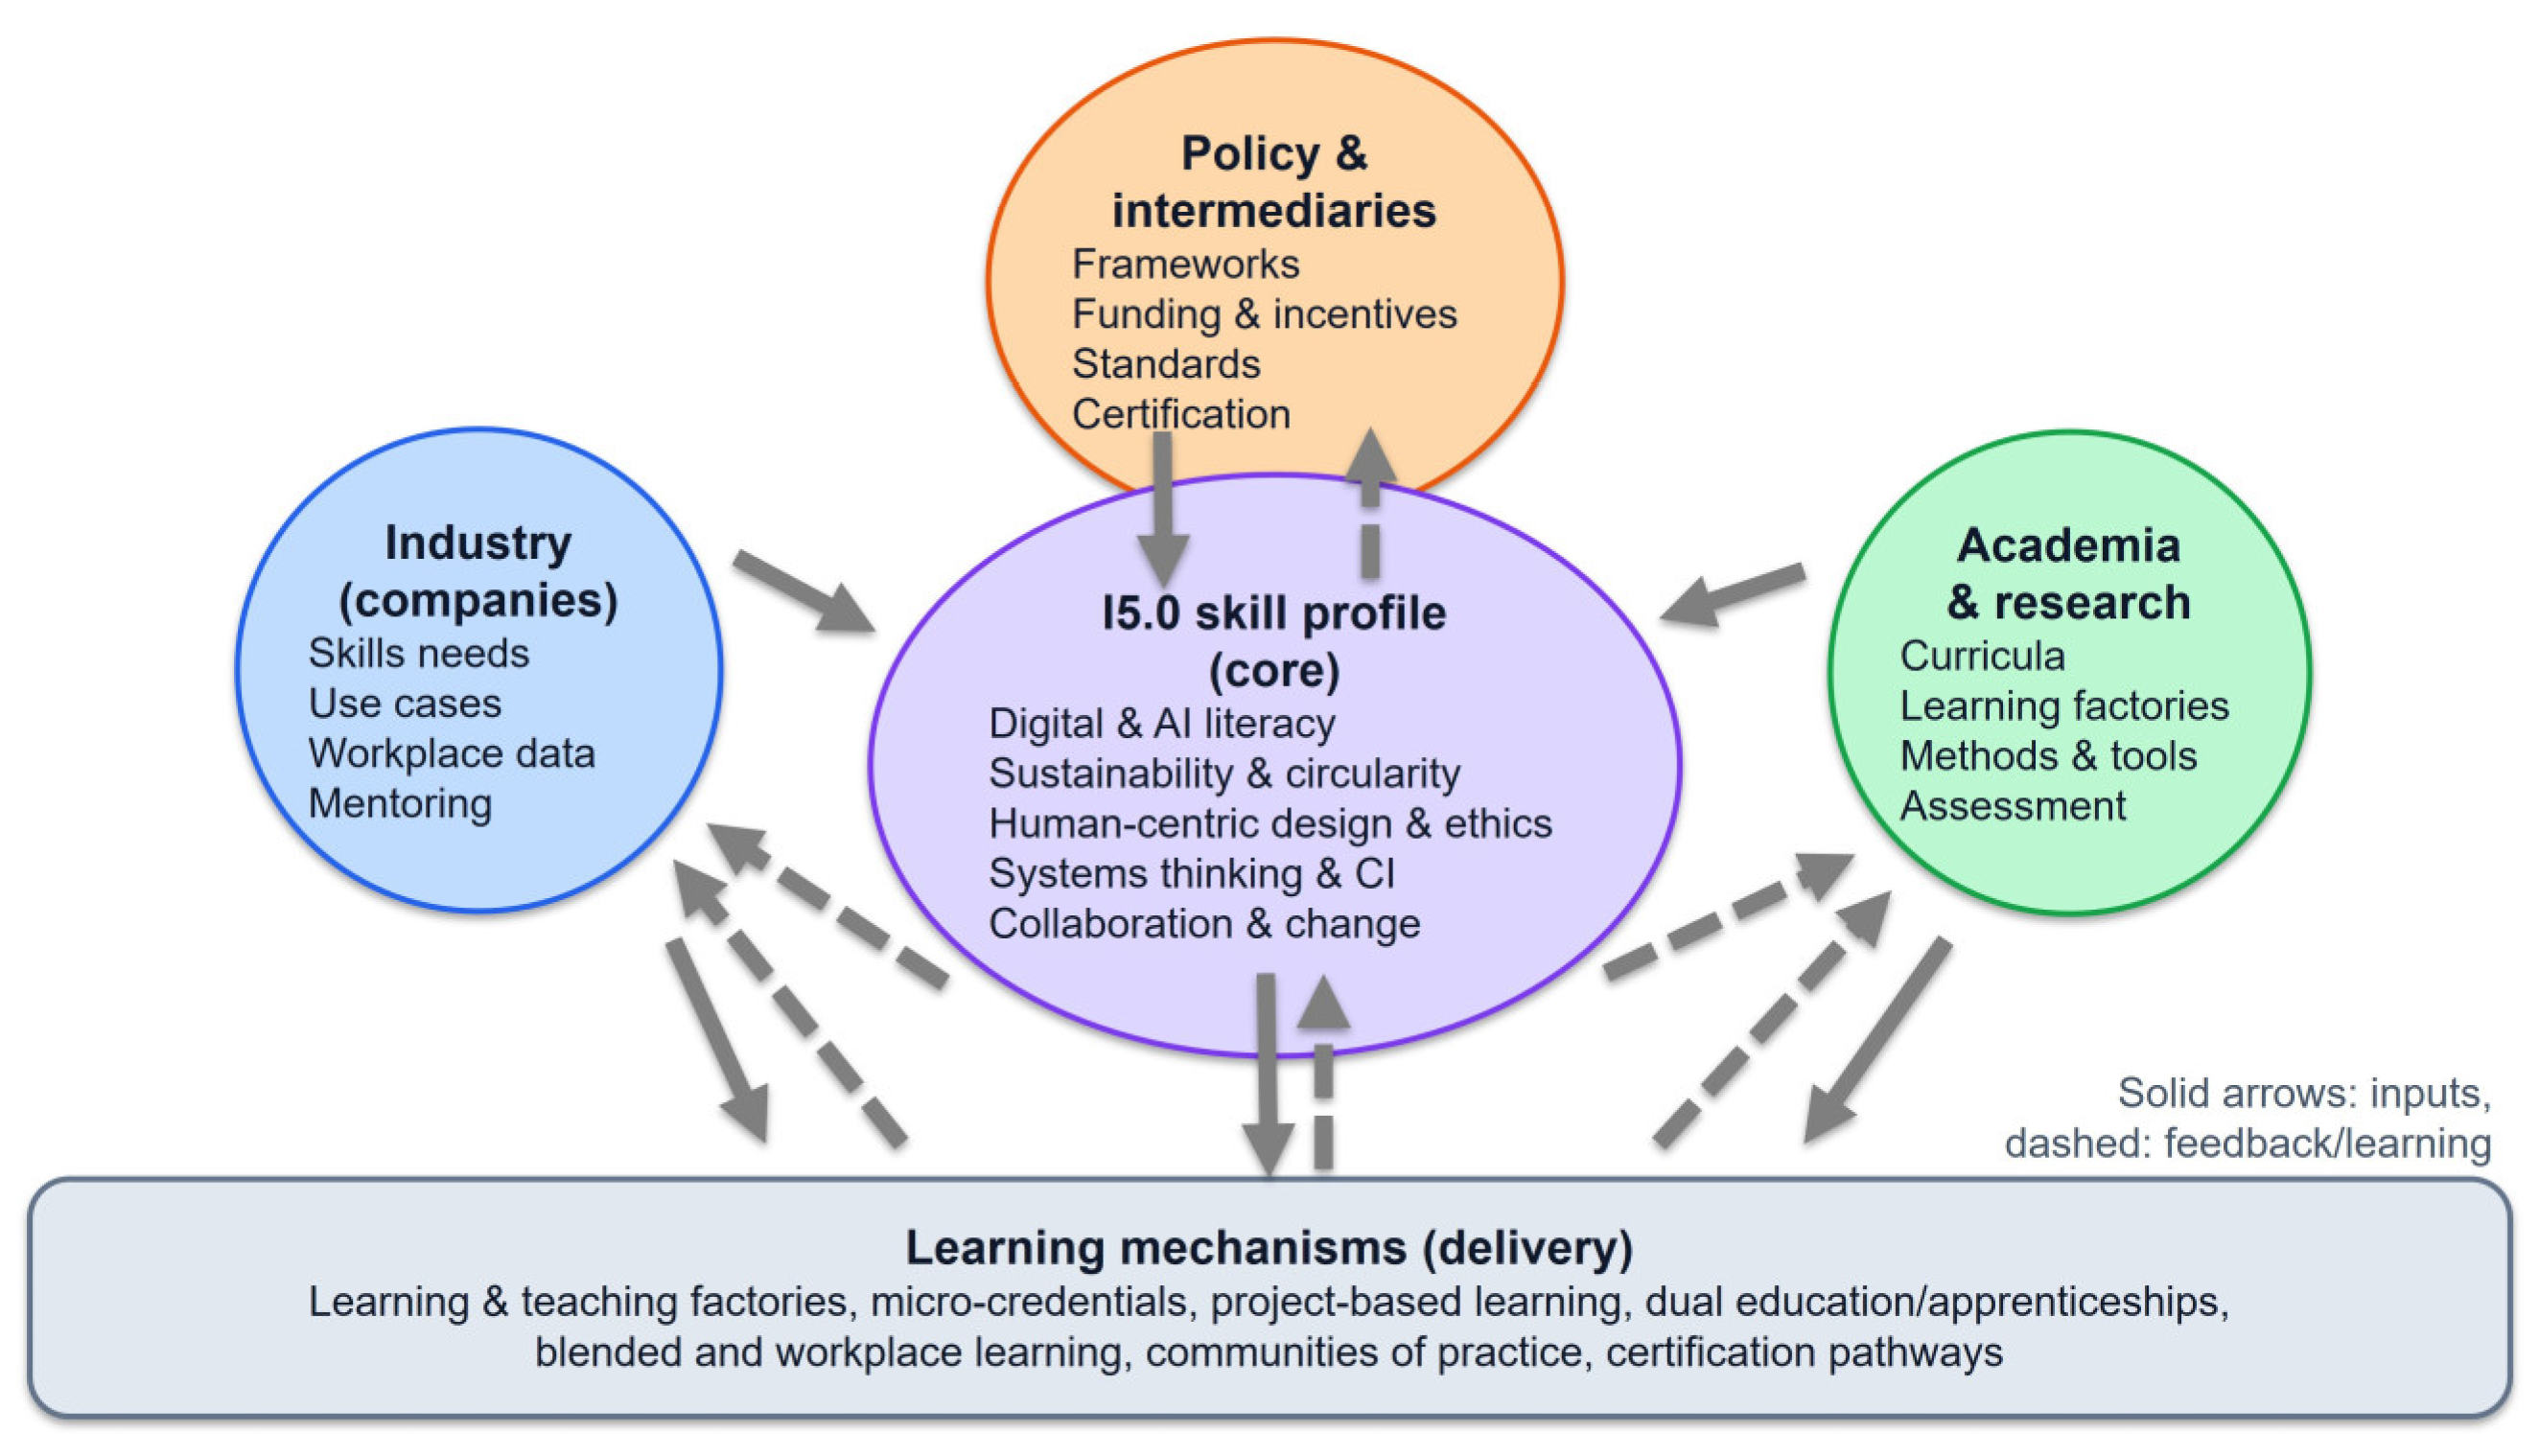
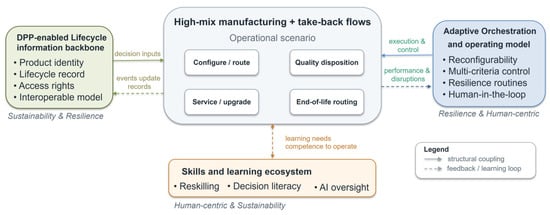
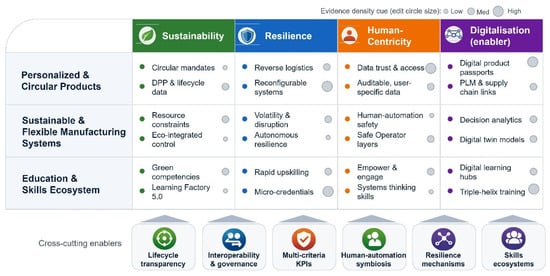
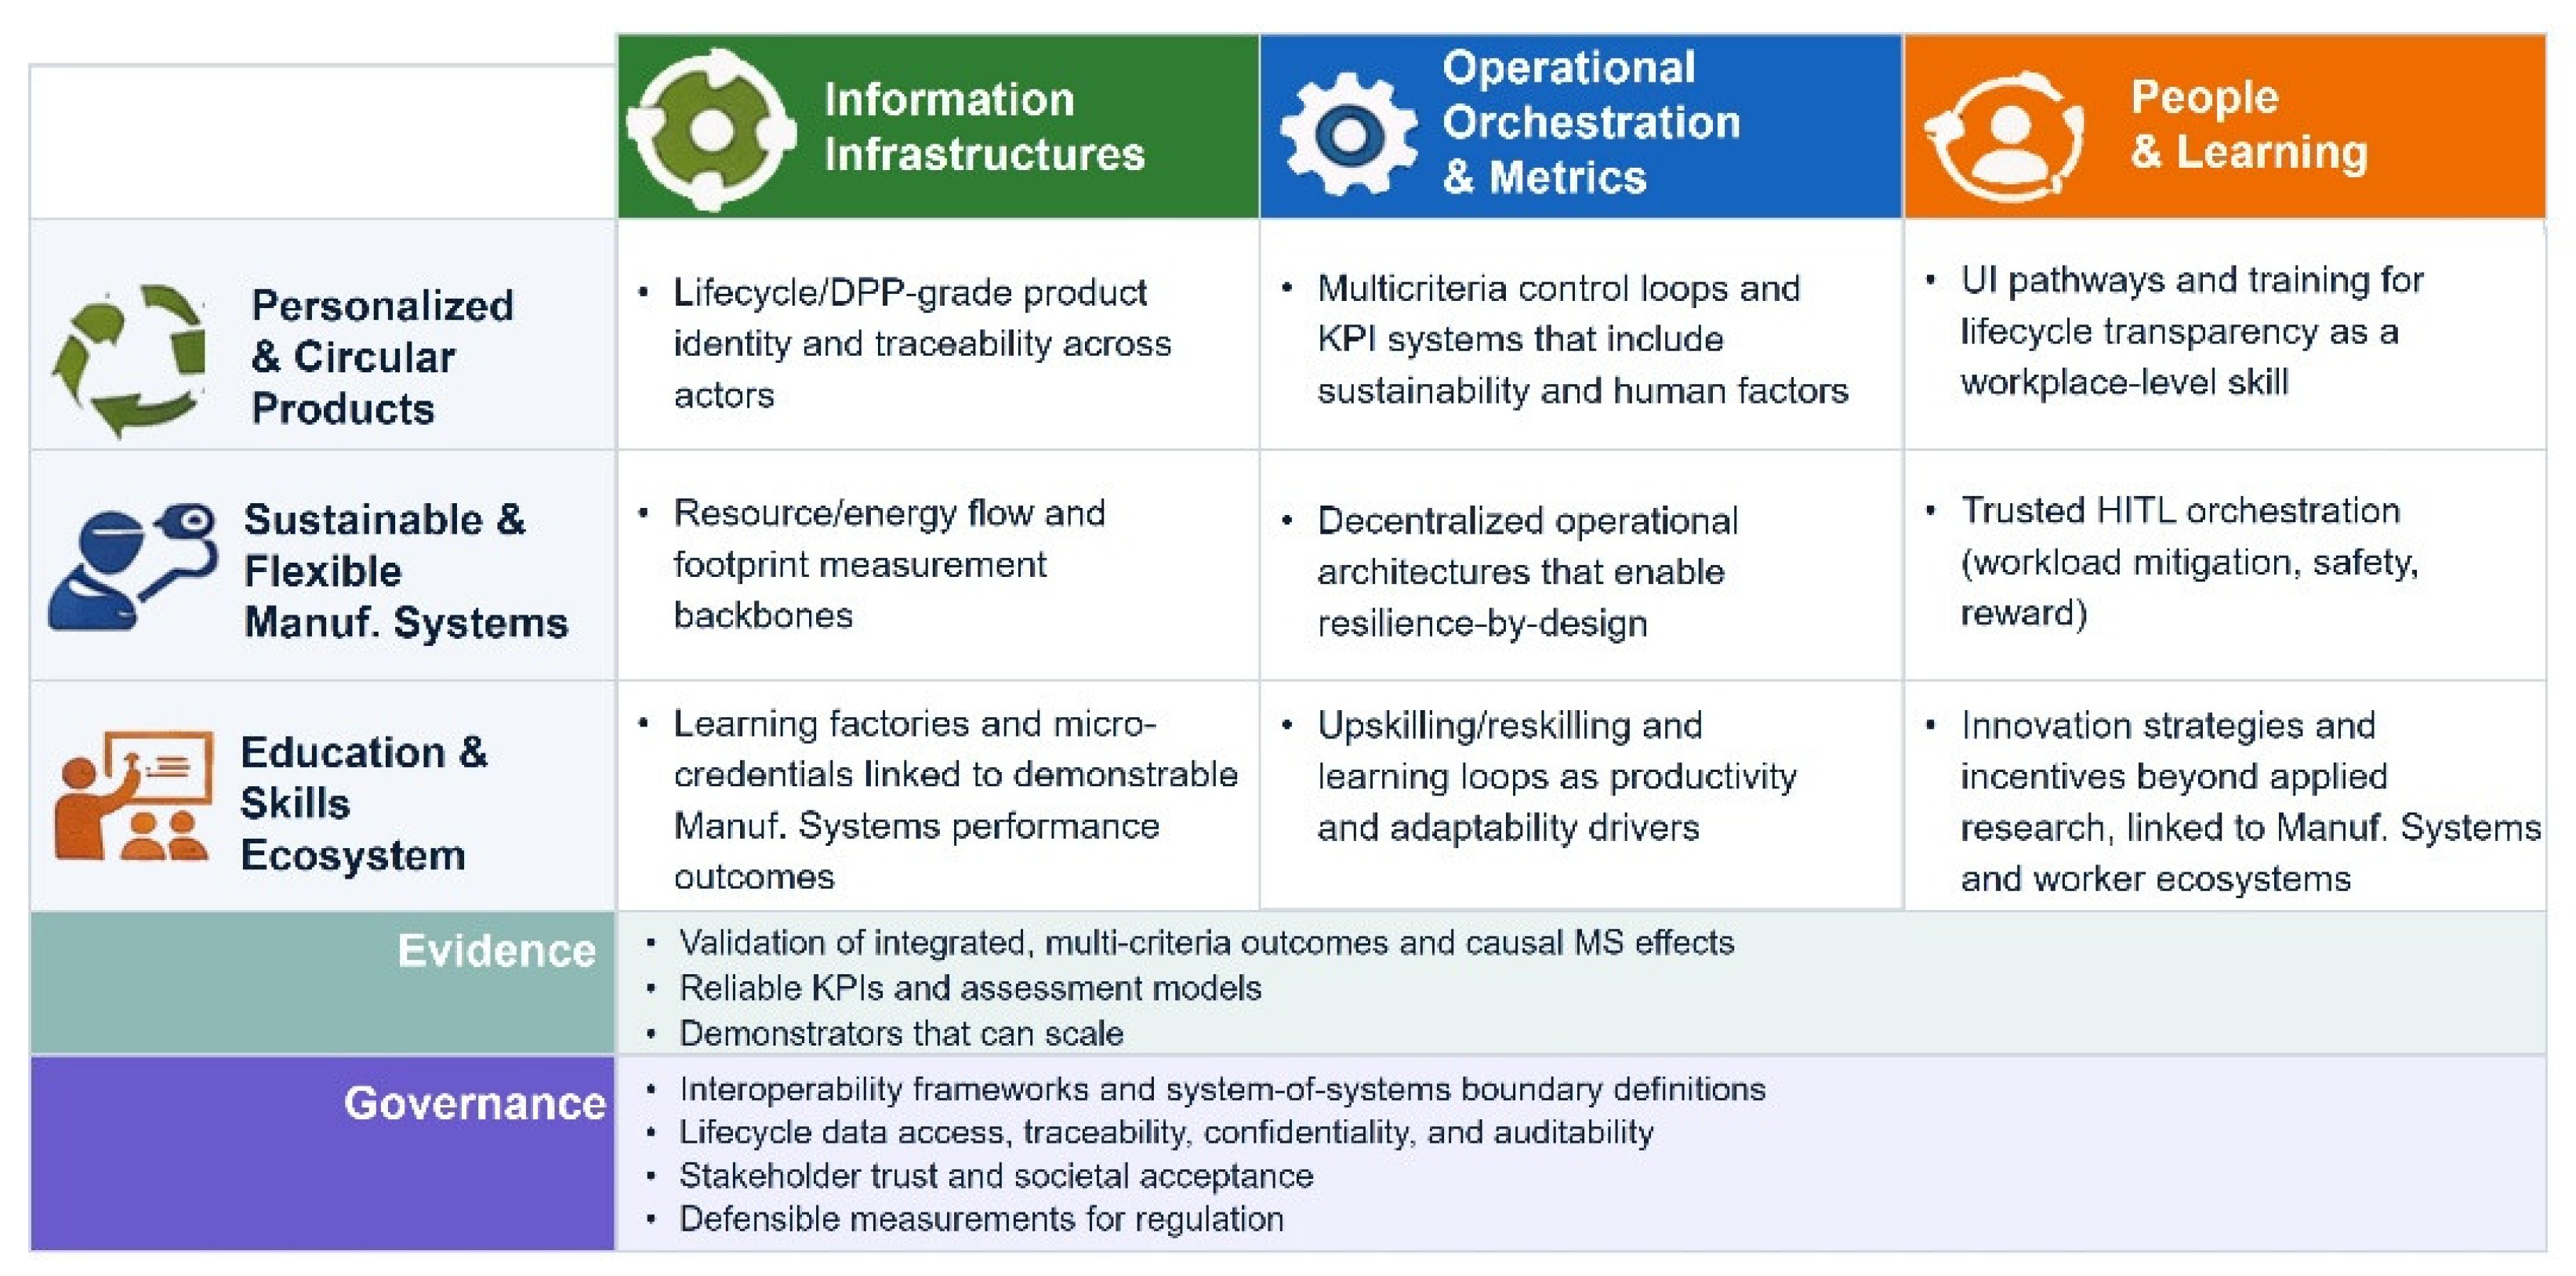
Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the author. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.