


Abstract
Wet stirred media milling (WSMM) is a popular grinding method used to produce important ultrafine-particle materials, such as pigments, pharmaceuticals, and pesticides. Therefore, it is crucial to improve the process capability and quality of WSMM by setting optimal parameters. This study proposes a multi-objective optimization methodology based on an intelligent algorithm to optimize the ultra-fine grinding parameters; this can mitigate the issue whereby grinding parameters are difficult to determine during wet grinding industrial production. A mechanistic model is proposed based on the analysis of energy dissipation mechanisms. The specific energy in the WSMM process is quantified using a stressing model. A shuffled frog leaping algorithm (SFLA)-based stressing model is proposed to maximize the specific stress intensity and specific stress number of the entire system under the constraint of the product particle size and grinding time, which provides the optimal process parameters. The performance of the proposed strategy is validated using two case studies in different industrial optimization scenarios. The result of the first case study illustrates that, in comparison to a quadratic programming-based response surface methodology, the proposed SFLA-based stressing model greatly enhances the wet grinding efficiency (decreasing P80 from 3.28 μm to 2.88 μm). In the second case study, the parameter optimization under different feed particle sizes and different productivities was discussed. The results confirmed that the optimized parameters can achieve the minimum particle size (P50 = 1.78 μm) and maximum solid concentration (Cv = 120 g/L) within the minimum grinding time (tg = 5 min). The contribution of our work lies in the fact that the proposed SFLA-based stressing model can direct multiple-objective decision-making in a more efficient way without requiring costly experimental procedures to acquire the optimized parameters in WSMM. The proposed approach is systematic and robust and can be integrated into WSMM architectures for parameter optimization in other complex wet grinding systems.
1. Introduction
Wet stirred media milling (WSMM) has become an established grinding technique for producing fine and ultrafine materials, such as foods, pharmaceutical products, pesticides, ceramics, and other materials [1,2]. Due to the very high stress intensity and number of stress events per unit time, energy is more concentrated in particle comminution, reducing ineffective energy consumption. Benefiting from the efficient concentration of energy, the specific energy consumption of WSMM is lower than those of tumbling and vibrating ball mills when producing micron-, sub-micron-, and even nano-scale particles [3]. Therefore, WSMM is a robust, reproducible, scalable, and environmentally friendly mechanized physical particle comminution process. WSMM is a complex process that is regarded as a “black box” [4]. It depends on several process variables, which can be divided into two categories: (1) mill parameters, such as the stirrer tip speed, mill volume, grinding media diameter, and density/filling ratio; (2) suspension properties, such as the solid volume concentration, viscosity, shear rate, flow rate, and particle size/Young’s modulus. In general, the diverse product properties and variety of available equipment make the process variables difficult to ascertain. Therefore, numerous parameters and uncontrollable factors make it challenging to optimize WSMM parameters [4].
Parameter optimization involves two aspects: (1) identifying the constraints of WSMM and (2) adjusting the input variables to obtain the desired performance. Many studies have attempted to identify the most important WSMM parameters and characterize and optimize the milling process. Kwade et al., Alamprese et al., and Hou et al. optimized WSMM parameters using a stressing model, response surface methodology (RSM), and a combined RSM-genetic algorithm (GA) approach, respectively [5,6,7,8]. These studies verified the feasibility of model-driven optimization; however, the former relied on extensive grinding tests to determine key parameters, while the latter two showed limited adaptability in multi-objective coupling scenarios. Based on a three-level Box–Behnken design, Celep et al. employed an RSM with quadratic programming (QP) for the modeling and optimization of process parameters during the ultra-fine grinding of refractory Au/Ag ores [9]. A second-order regression model was fitted to experimental data and then optimized using the quadratic programming method to minimize the d80 size within the experimental range studied. Mäntynen et al. proposed a three-step optimization procedure for the production of colorant paste. First, a Plackett–Burman experimental design was used to determine the most significant grinding variables. Second, quadratic models of tinting strength and grinding power were constructed, and finally, a set of Pareto-optimal solutions was obtained based on the lower and upper limits of the corresponding grinding conditions [10].
Using an enhanced stress model, Breitung-Faes et al. predicted the optimum parameters for inorganic nanoparticle production by WSMM. By analyzing the relationships between the average optimum stress energies and single-particle-breakage variables of different product materials, an optimum set of parameters can be obtained. However, comparative analyses of grinding capabilities under optimal parameters remain lacking [11]. Using residence time distribution modeling, Montalescot et al. studied the hydrodynamics involved in WSMM. Stress intensity–stress number (SI–SN) modeling has been successfully applied to microalgae production, with its operating parameters optimized to minimize energy consumption [12]. Based on a three-factor, three-level, and face-centered CCD, Nekkanti et al. studied the effects of bead milling process variables on the manufacturing process of drug nanoparticles. The variables investigated were the motor speed, pump speed, and bead volume, and the responses were the milling time, particle size, and process yield. The optimum process was obtained using Design-Expert ® (version. 7.3.1; Stat-Ease Inc., Minneapolis, MN) program to evaluate both the repeatability and reproducibility of the bead milling technique [13]. Flach et al. evaluated the characteristic parameters of a stress model and a micro-hydrodynamic model for the process optimization of a nanosuspension prepared by WSMM. They showed that process optimization resulted in the same optimum set of operating parameters. However, comparative analyses of the influence of optimized parameters on the mill grinding capacity are lacking [4]. Brunaugh et al. argued that micronization, such as that achieved by stirred media milling, is well-suited to parameter optimization, due to its generally low-yield high-energy consumption process. They reviewed the optimization of pharmaceutical milling parameters through design space development, theoretical and empirical modeling, and the monitoring of critical quality attributes [14]. Katircioglu-Bayel. studied the effects of operating parameters on the product particle size, surface area, and energy consumption. The optimum process parameters were determined through numerical calculation and correlation analysis [15]. Santosh et al. studied the effects of the stirrer speed, grinding time, feed size, and solid concentration on the product size and energy consumption when grinding the chromite ore-bearing platinum group of elements in a laboratory stirred mill. Two regression process models were developed and optimized using quadratic programming and Design Expert software [16]. Katircioglu-Baye et al. investigated the impact of four factors (the stirrer speed, grinding time, media filling ratio, and solid mass fraction) on the product particle size (d50). By using the three-level Box–Behnken design, the optimum operating parameters for minimizing the d50 size were determined [17]. Amini et al. proposed a response surface methodology (RSM) to determine the optimum parameters for extracting phenolics from pomegranate peel [18]. Guner et al. studied the influence of bead sizes and bead mixtures on breakage kinetics during the nanomilling of drug (griseofulvin) suspensions. The experimental results show that the use of bead mixtures did not lead to notable process improvements, and 100 µm beads outperformed bead mixtures with the advantages of fast breakage, low power consumption, and heat generation [19]. Wang et al. established the relationship between the grinding power consumption and operating parameters in a tower mill based on the BP neural network optimized by the GA to obtain the optimum conditions [20]. BAHETI et al. used canonical analysis with the help of SYSTAT software (https://www.grafiti.com) to optimize the model equation and determine the optimum conditions for operating parameters of high-energy planetary ball mills [21]. Gbadeyan et al. analyzed the signal-to-noise (S/N) ratio to determine the optimum process parameters in nano calcium carbonate production [22]. Guo et al. used response surface methodology (RSM) to optimize the three key process parameters based on the grinding technology efficiency as the evaluation criterion. They found that the order of significance of the parameters affecting the grinding efficiency was as follows: grinding time > media filling rate > stirrer speed [23].
Table 1 provides an overview of current research on the topic.
Table 1.
Literature summary on process optimization in WSMM.
From the abovementioned literature, we identified three main issues in implementing WSMM parameter optimization.
(1) The goal of parameter optimization is to understand the fundamental behavior of WSMM. Currently, WSMM parameter optimization relies heavily on empirical approaches, experimental design, and modeling based on the first process [16]. However, WSMM is expensive due to its low mill capacity and high energy consumption [24]. Therefore, reducing the experimental cost and improving the optimization results remain challenging.
(2) Parameter optimization in WSMM usually involves multi-objective optimization (MOO) to characterize the product quality in response to variations in the input. Stress models and RSM are currently the most widely used parameter optimization strategies. However, these models rely on experience or theoretical analysis, while optimization analysis depends heavily on experimental data [6]. Due to the diversity of product quality attributes, which are sometimes contradictory and conflicting, stress models and RSMs need further development for use in MOO.
(3) Few studies in this field have used intelligent algorithms. These are metaheuristic algorithms, which generally do not require the continuity and convexity of the objective function and constraints. They have high adaptability to data uncertainty and are regarded as potentially powerful tools for solving MOO problems [25]. However, their application to WSMM parameter optimization requires further study.
The goal of this study is to address these three issues. To achieve this, a parameter optimization methodology is proposed based on a stressing model and intelligent algorithm.
2. Materials and Methods
2.1. Materials
Heavy calcium carbonate (HCC), which is widely used in daily chemical industries such as rubber, plastics, papermaking, paints, inks, cables, and building supplies, is employed as an experimental material in the second case study. The specific gravity of the HCC was determined to be 2.80 g/cm3. The HCC sample was ground in laboratory rod mill at 50–120 g/L pulp density with different mono-sized fractions (50% passing size, D50 = 6–32 μm) and riffled to obtain 60–130 g representative sub-samples prior to ultrafine grinding using the pin-type horizontal stirred mill (RTSM-05, Anhui Root Intelligent Equipment Co., Ltd., Suzhou City, Anhui Province, China). The earlier chemical and mineralogical analysis studies carried out on HCC samples are shown in Table 2.
Table 2.
Analysis of HCC elements in samples.
On the other hand, an antimonial refractory gold/silver ore sample was obtained from Akoluk (Ordu, Turkey) and used as a grinding material. It was determined to be rich in silver, containing 220 g/ton Ag and 20 g/ton Au. Its main chemical composition is shown in Table 3 [9]. The material was ground at a 50% pulp density for P80 = 60 μm prior to ultrafine grinding using a wet stirred mill [9].
Table 3.
Chemical composition of the grinding material [9].
2.2. Methods
2.2.1. Energy Dissipation Mechanism in WSMM
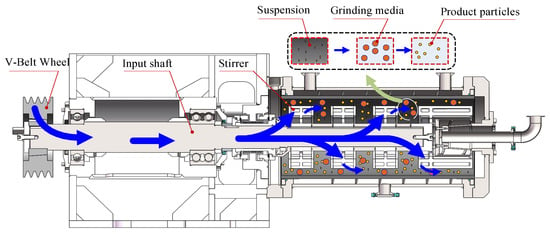
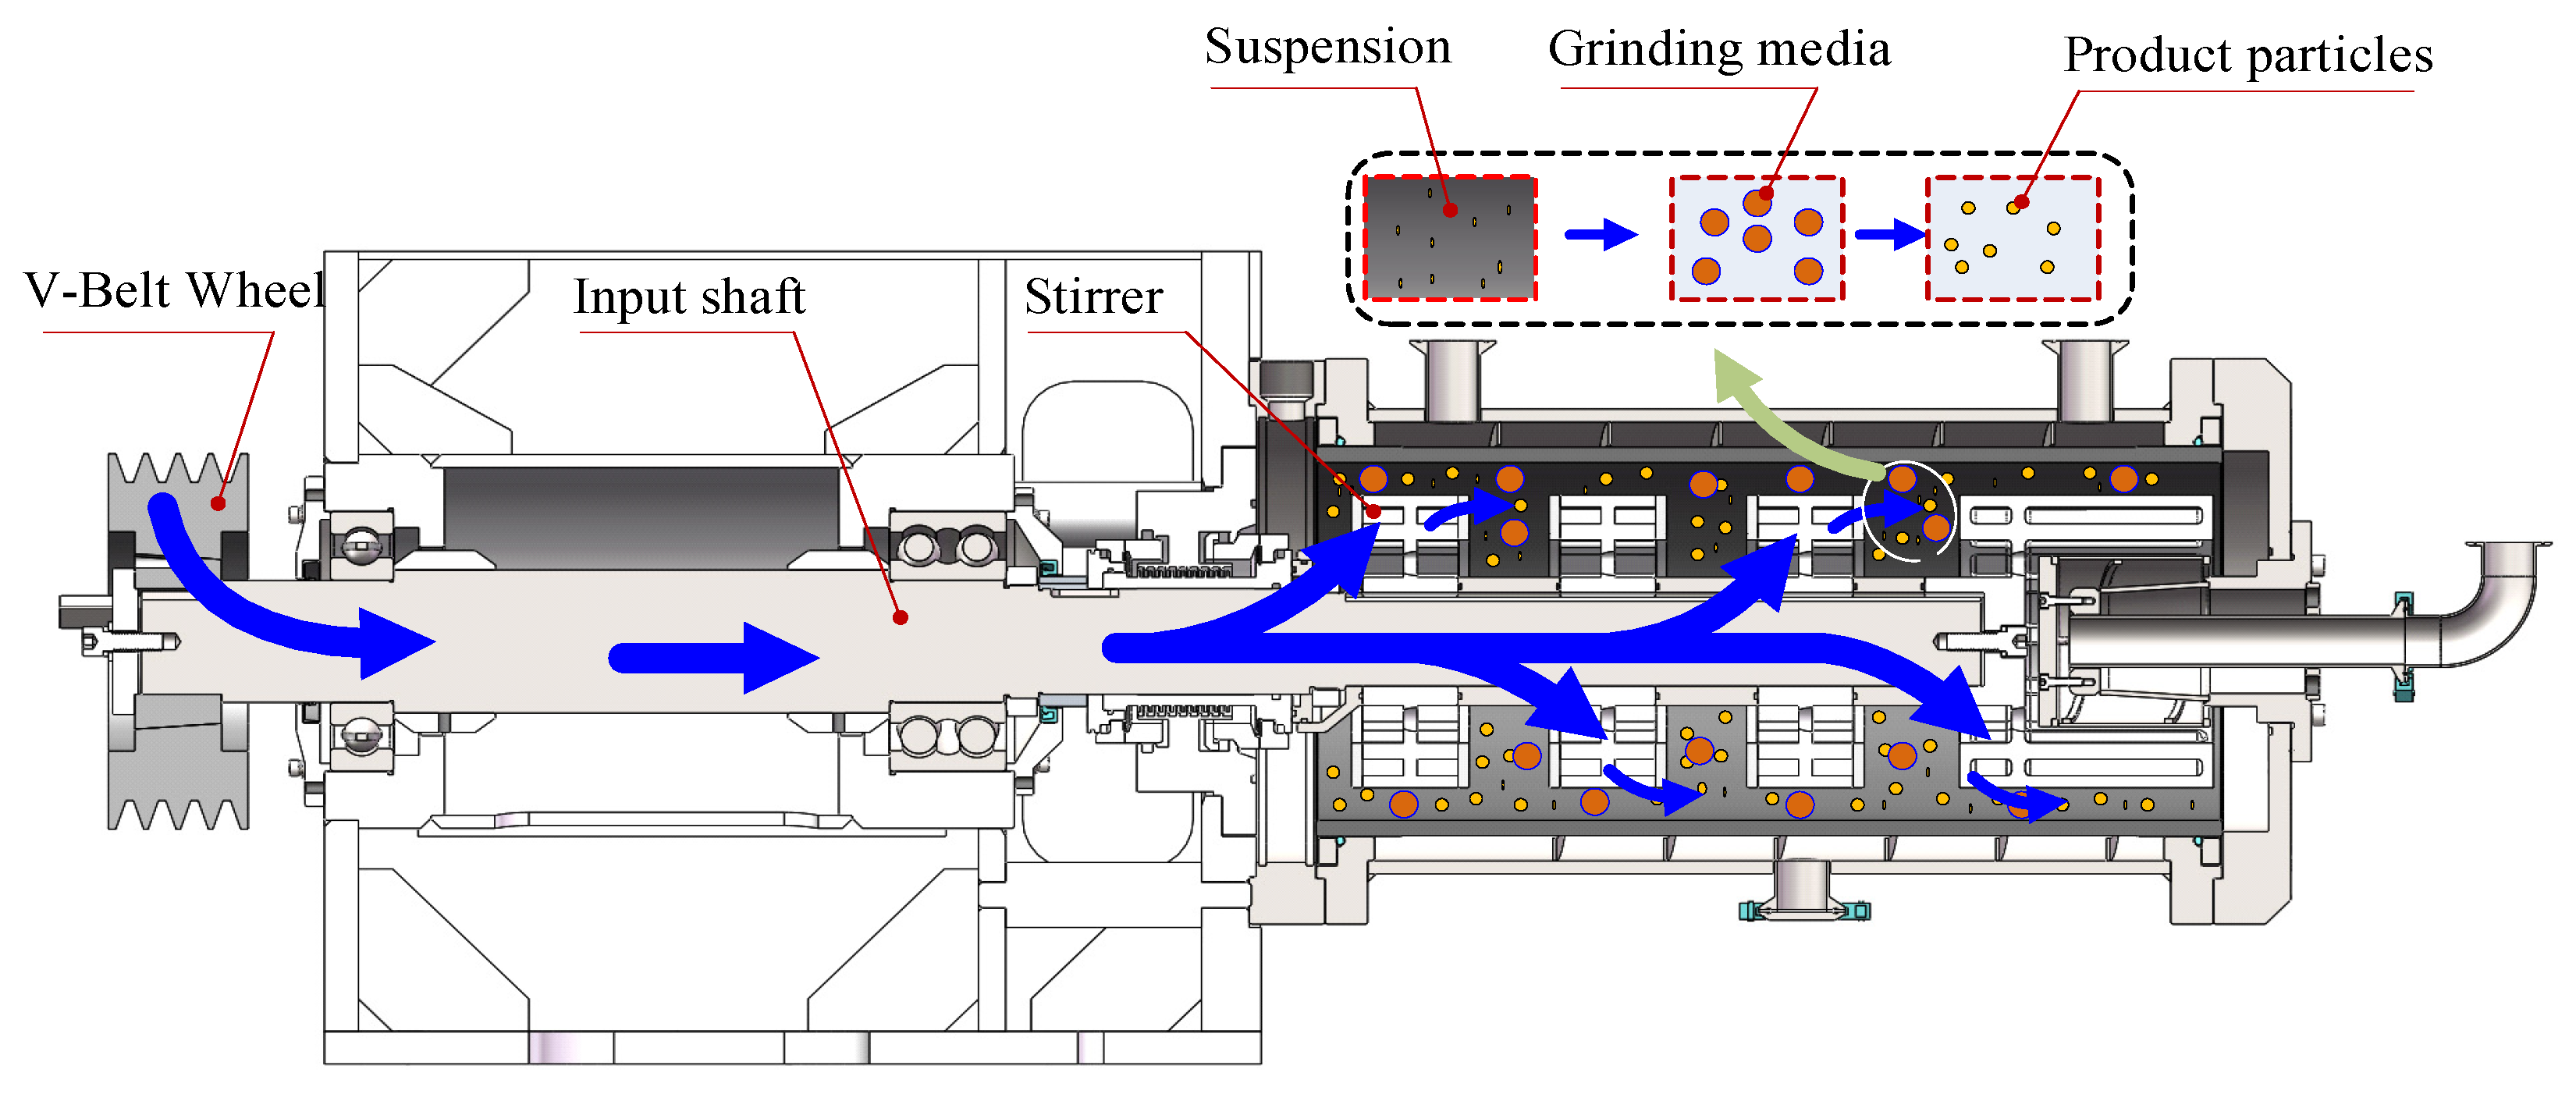
In actual comminution processes, the performance of WSMM is contingent on the total energy transferred to the product particles. Though there are many different types, geometries, and sizes of products made by WSMM in various industries, the operating principle remains similar: a motor drives a stirrer, which stirs a suspension. Energy is transferred from the suspension to the grinding medium, and the dominant particle breakage mechanism is shear and friction between grinding media, rather than normal impact—this is particularly evident in the ultra-fine grinding of materials [26]. To analyze the mechanical energy absorbed by particles, it is essential to analyze the energy dissipation mechanism of the energy transfer process. Figure 1 provides a schematic overview of the energy dissipation mechanisms of WSMM.
Figure 1.
Schematic overview of energy dissipation in WSMM.
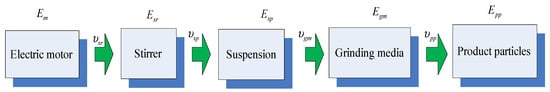
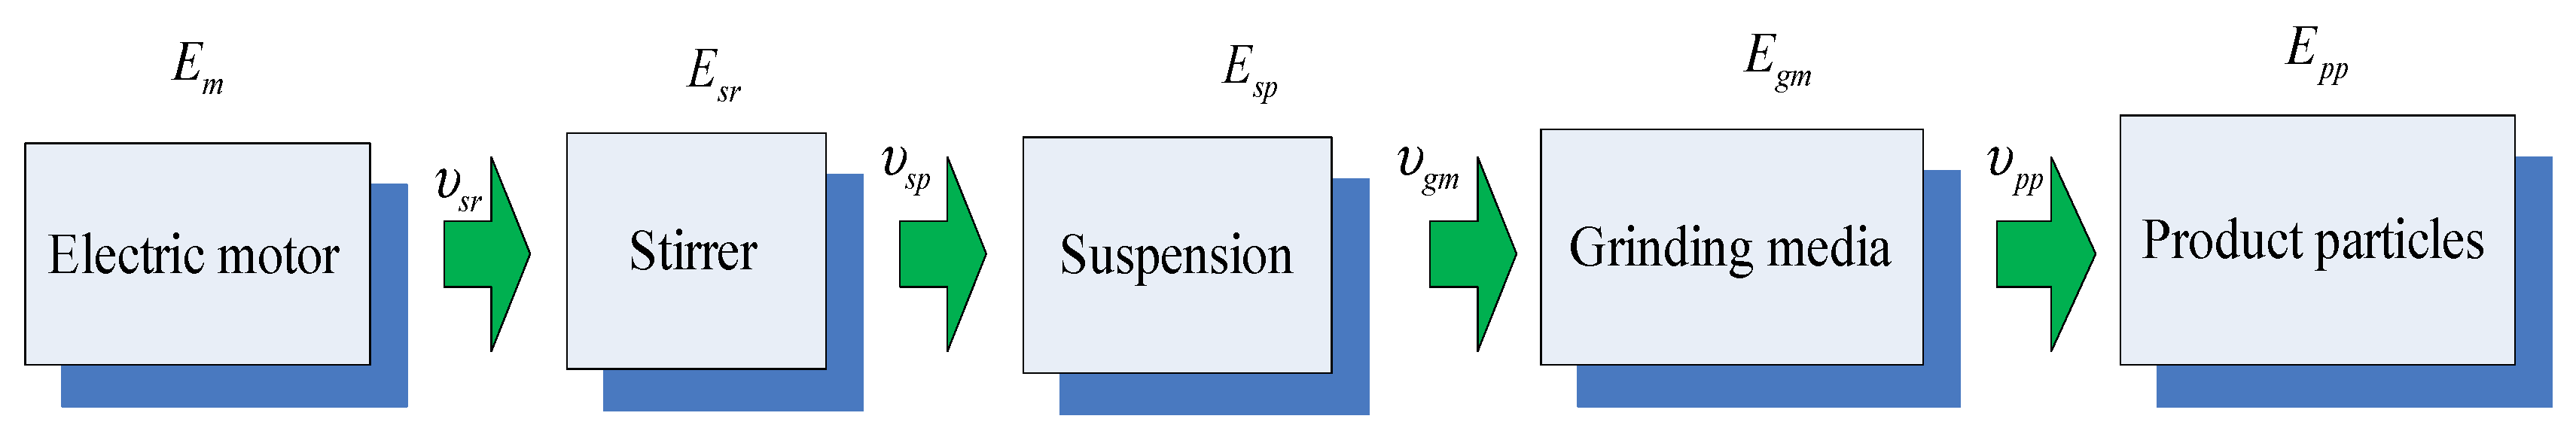
Energy transfer and dissipation among the various components of WSMM processes, such as the input shaft, stirrer, suspension, grinding media, and product particles, can be regarded as largely linear continuous processes, although coupling exists locally. In terms of particle stress, certain coupling effects can be ignored, for example, the dynamic effect of the grinding media on the suspension. The comminution result is determined by the energy transferred from the grinding media to the product particles [5]. However, only a small part of the input energy of the chamber is used for particle stressing [5]. Figure 1 shows that the energy introduced to the chamber experiences a large amount of dissipation before reaching the product particles. The energy dissipation process is illustrated in Figure 2, in which blue arrows represent the direction of energy transfer.
Figure 2.
Energy transfer and dissipation process.
In Figure 2, Em is the specific energy provided by the electric motor, which transfers energy to the stirrer via the V-belt wheel and input shaft, as shown in Figure 1. is the energy transfer coefficient, which is the percentage of kinetic energy transferred from the electric motor Em and consumed by the stirrer Esr. can be estimated according to Equation (1).
Here, P and P0 represent the electric motor power and the power consumed by the stirrer, respectively. The stirrer also outputs energy to the suspension. The energy consumed by the suspension, Esp, is expressed as Equation (2).
where is the energy transfer factor of the suspension. The energy is dissipated by liquid friction and facilitates dispersion but not particle stress. The energy is related to the viscosity, shear rate, and volume fraction of the suspension and is dissipated as heat and vibration due to shear friction inside the suspension [5]. Like the stirrer, the suspension also transfers part of the energy to the grinding media via liquid–grinding media, viscous friction, and lubrication. This energy component is also divided into two parts: the non-particle-stressing energy Egm and particle-stressing energy Epp. Similar to Equation (2), if the energy transfer factor of the beads is given, Egm can be calculated using Equation (3).
The non-particle-stressing energy Egm is dissipated as heat and vibration in two main ways: (1) The suspension is displaced by approaching grinding media, wherein the kinetic energy is reduced due to viscous damping by the suspension. (2) The grinding medium contacts product particles without stressing them [4]. The particle-stressing energy Epp, which is the energy used in particle crushing, is mainly manifested by grinding media wear and deformation, and is a function of the particle–grinding medium elasticity ratio [27]. Similar to Equation (3), Epp is calculated according to Equation (4).
Here, is the energy transfer factor, and Epp is the specific energy delivered to product particles. If the ith stress intensity SIi and the frequency distribution SFi of all stress events are given, then Epp can be written as
where and are the average stress intensity and total stress number of product particles, respectively.
2.2.2. Parameter Optimization Using the Stressing Model
The distribution of the stress intensity will not change as long as the geometry of the chamber remains unchanged. By taking into account the elastic modulus of the grinding media and product particle materials [27], the stress intensity of the grinding media in a single stress event, SIgm, can be defined as follows:
where , , , and are the diameter of the grinding beads, stirrer speed, stirrer diameter, and grinding media density, respectively. and are the Young’s moduli of the product and grinding media, respectively. Since the linear velocities of the grinding media in the chamber are different, so is the stress intensity. Introducing the stress intensity factor , the average stress intensity of the product particles, , is determined as
In addition to the stress intensity, the stress number SNgm denotes the number of stress events, and is defined as follows [28].
where , , , , and are the stirrer rotation speed, effective volume of the chamber, grinding media filling level, porosity, and grinding time, respectively. In a multi-pass continuous grinding process, if the total volume of the suspension to be ground is , and the flow rate of the suspension is , the grinding time can be derived as follows:
where k is the number of times the suspension has been ground. Since not all grinding media can capture product particles in every stress event, given the stress number factor , the total stress number that the grinding media can capture the product particles, , can be determined as follows.
Combining Equations (5)–(8), the specific energy can be derived:
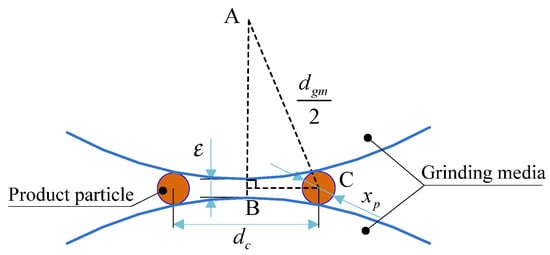
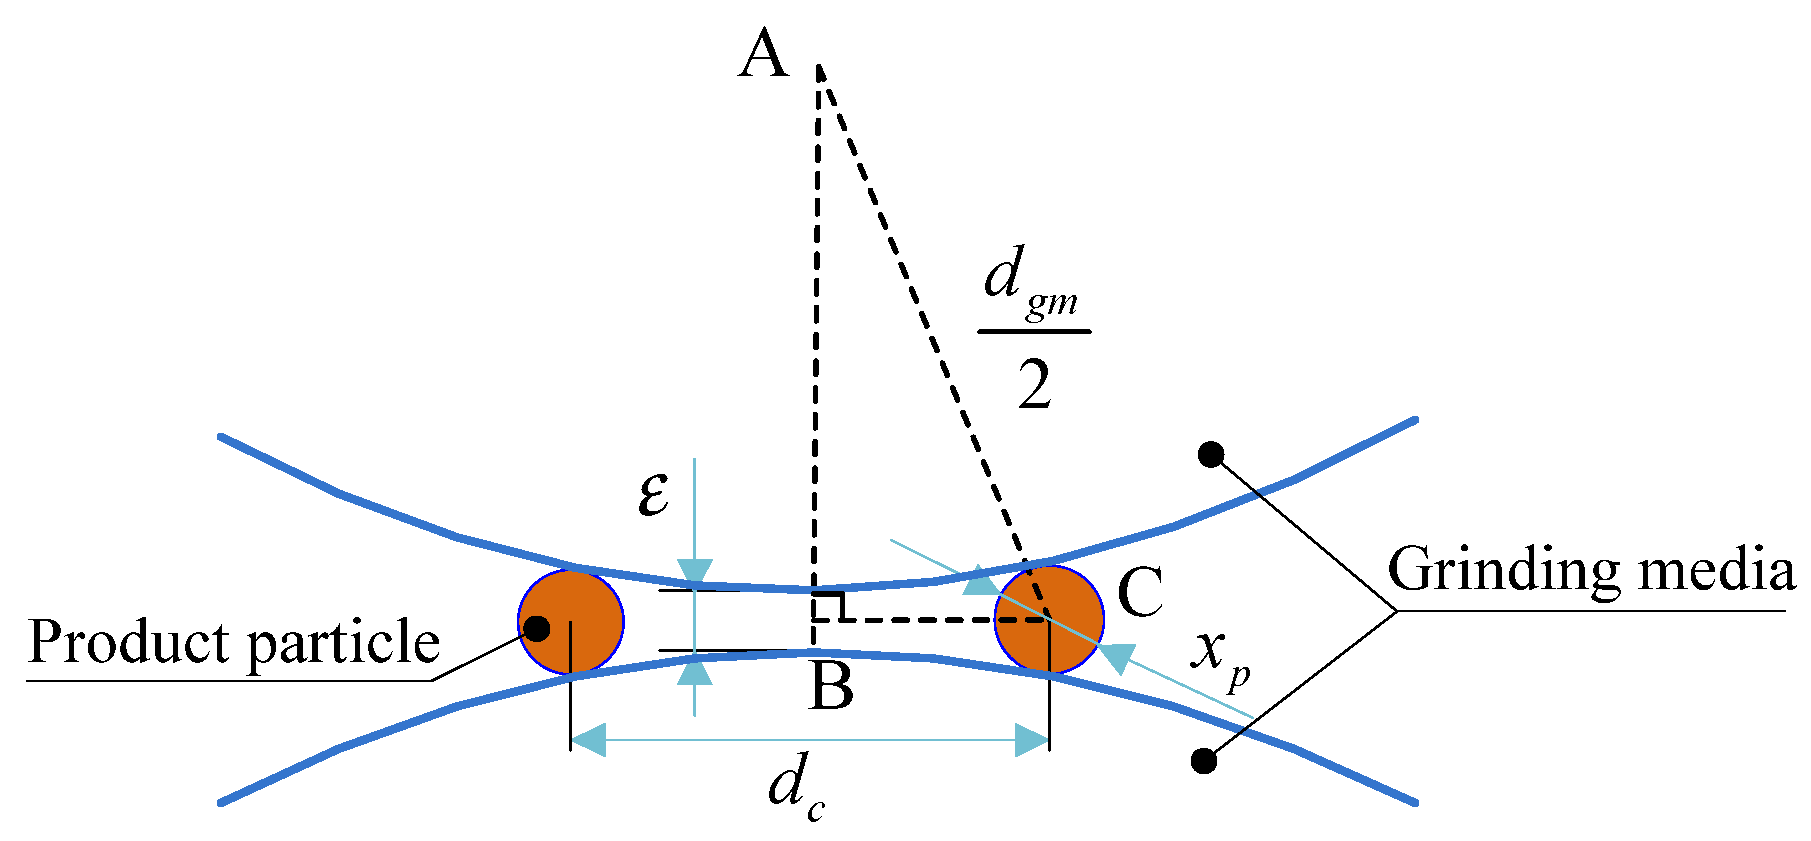
where is the total energy transfer coefficient. Since more than one particle is captured by the grinding media in each stress event, it is necessary to calculate the stress intensity and stress number of a single particle. Figure 3 shows a scenario where two product particles are stressed by two grinding media. In the actual grinding process, the number of product particles captured depends on the active volume between two grinding media in a stress event [29]. This active volume is proportional to the diameter of the grinding media and that of the product particles.
Figure 3.
Active volume calculation.
Figure 3 shows the spatial relationship between grinding media and product particles. The orange circles denote product particles, which have a diameter of xp. The minimum distance between the grinding media is ε, and dc is the diameter of the active volume. According to the triangle ABC, dc can be calculated as
when ε = 0, and xp and dgm are constants. dc takes the maximum value of . The active volume Vc can be derived as follows:
If the solid concentration of product particles Cv is given, then the stress intensity per unit product quality in a stress event can be estimated according to Equation (14).
Similarly, the number of stress events per unit product quality, SNp,s, can be found using the following equation:
where mp is the mass of product particles in the chamber, and Vc is the volume of the chamber. To improve the grinding efficiency, it is necessary to increase the stress number per unit time and the stress intensity . Further, the product particle diameter xp must be limited to a certain range, . Mathematically, this can be expressed as
where is the slurry flow rate. , , and k represent slurry flow rate coefficients.
2.2.3. Optimization Strategy Using the Intelligent Algorithm
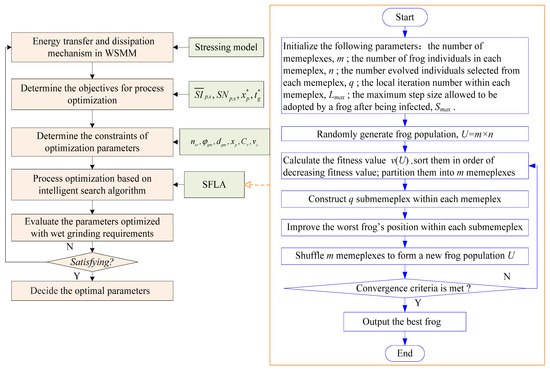
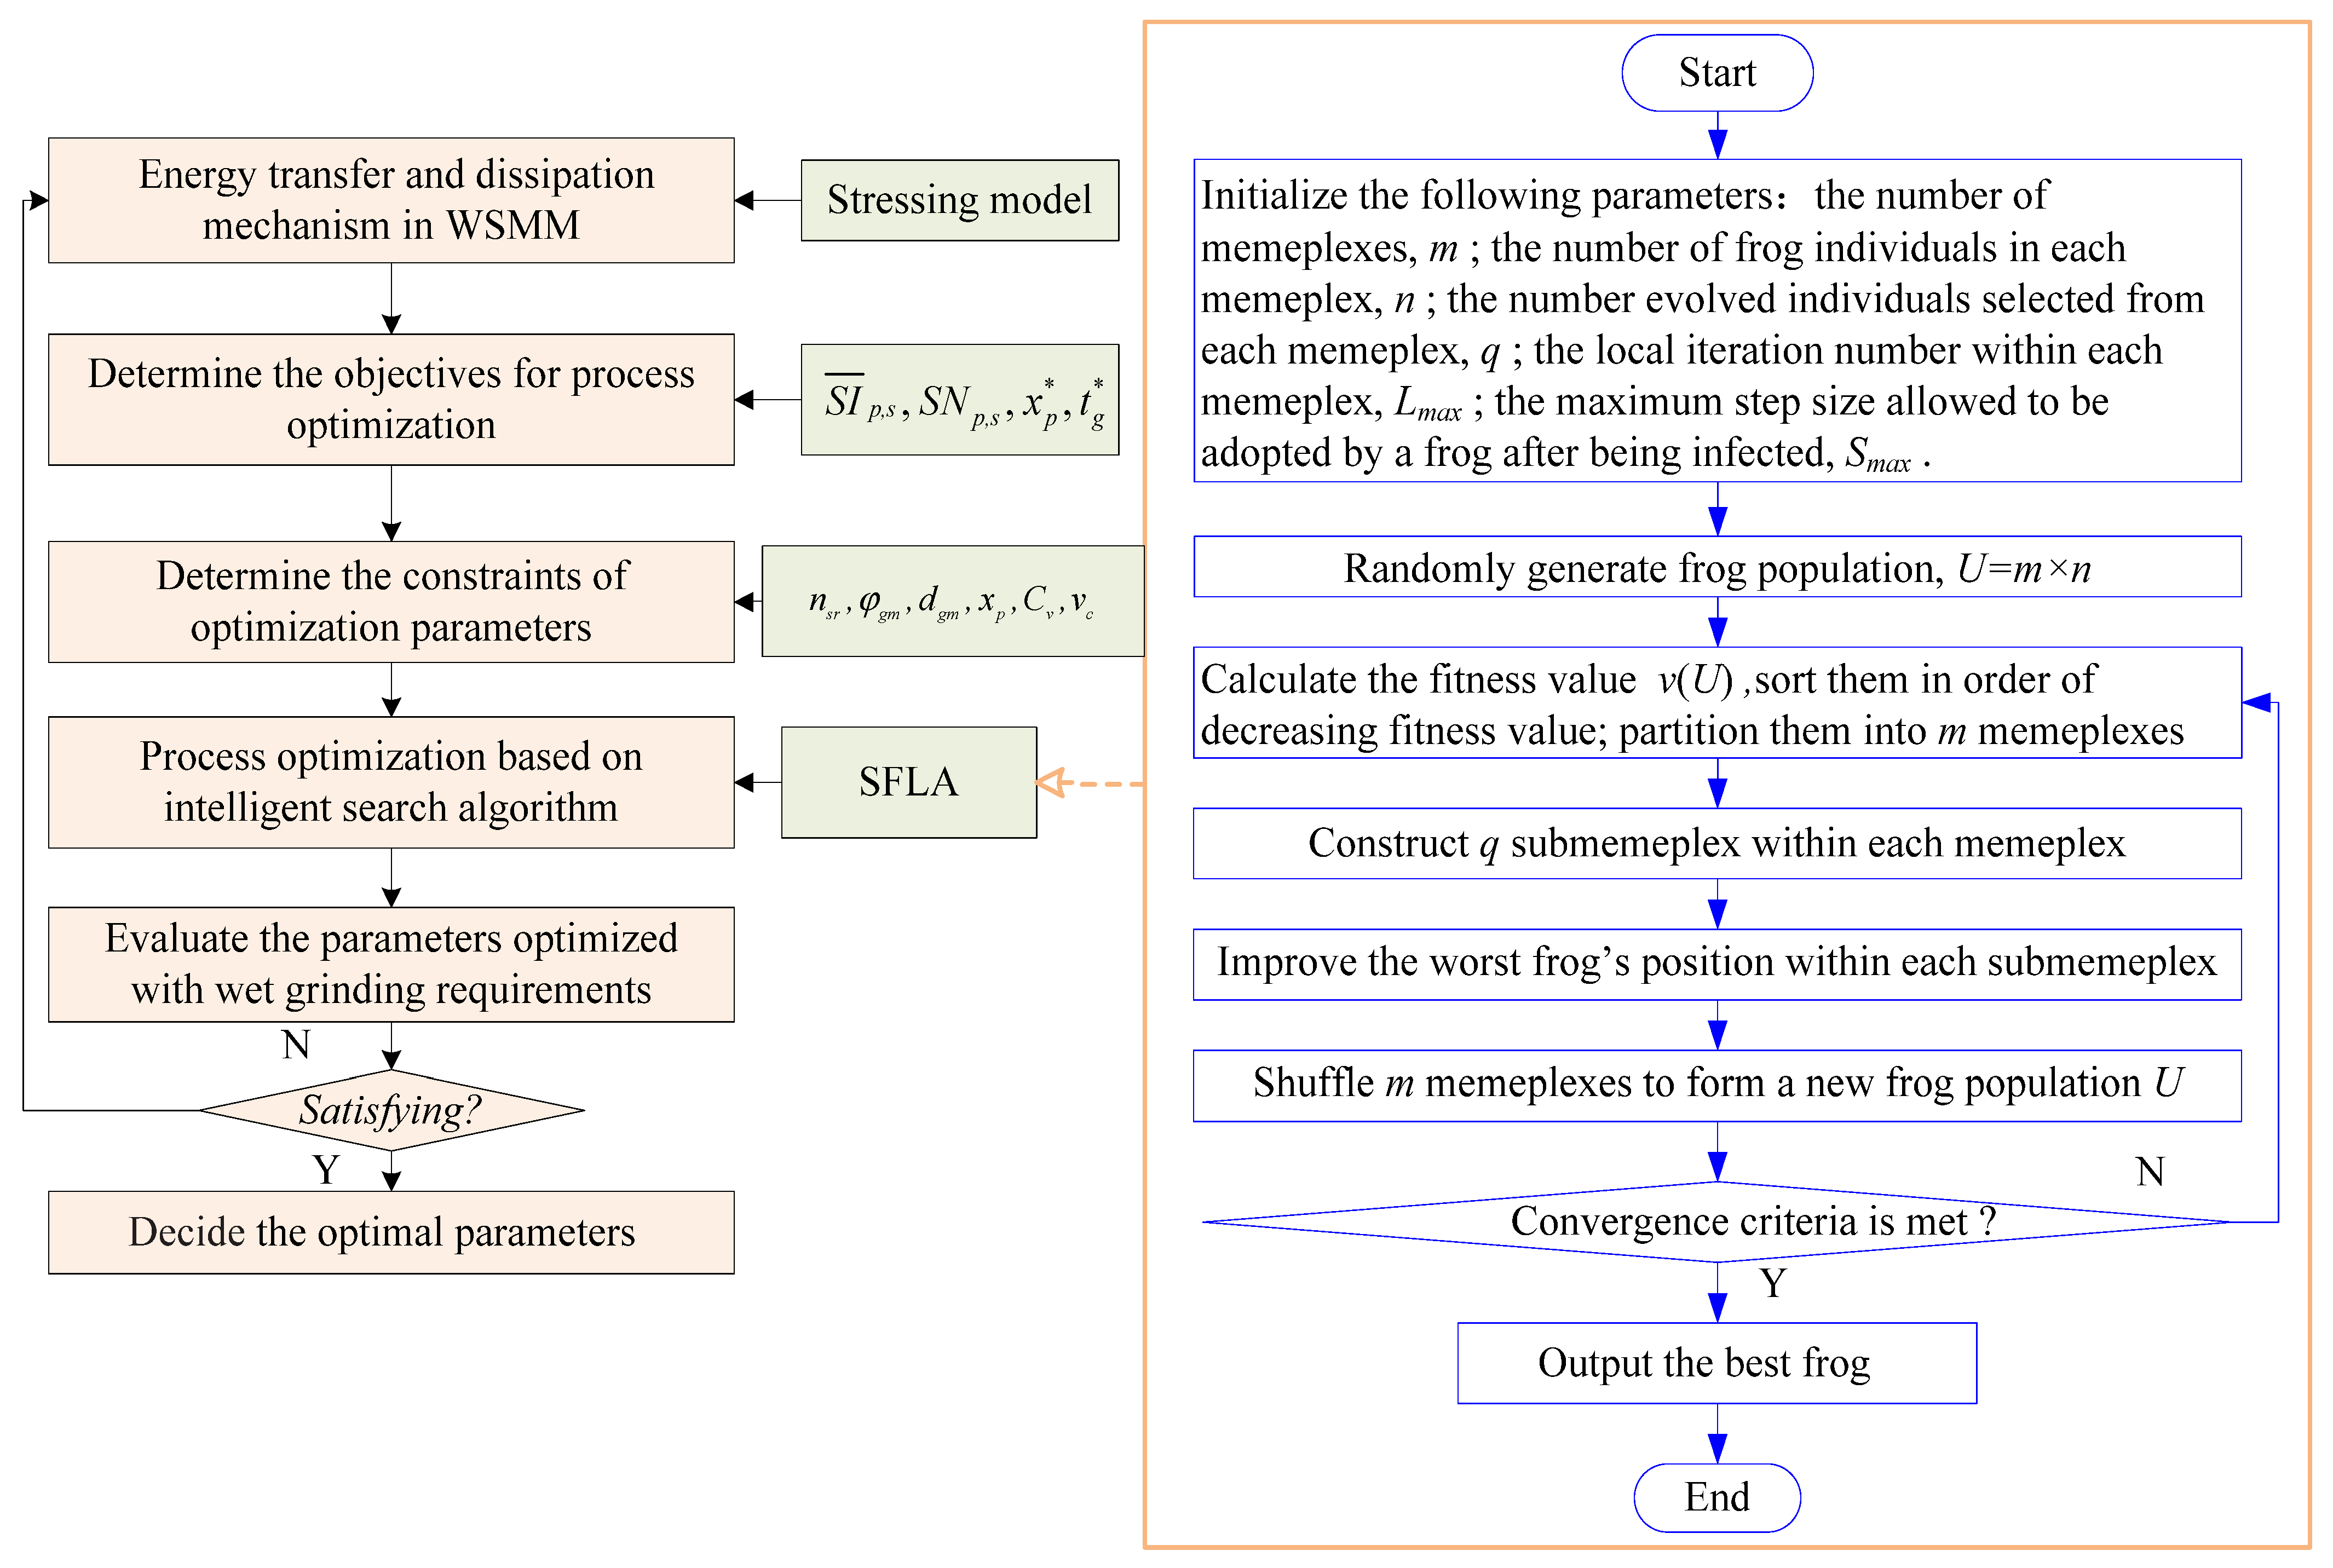
Process optimization problems are actually multi-objective optimization (MOO) problems. Under MOO conditions, the optimized process parameter set is, in fact, a Pareto-optimal set. Conventional mathematical programming (MP) is generally employed to solve such problems, which is sensitive to the Pareto-optimal frontier and requires the objective function and constraints to be differentiable [30]. In contrast, the meta-heuristic algorithm is not subject to such restrictions and is regarded as a powerful tool for solving MOO problems [31]. Therefore, a meta-heuristic algorithm—the shuffled frog leaping algorithm (SFLA)—is developed for process optimization in WSMM. The SFLA combines the merits of shuffled complex evolution (SCE) and particle swarm optimization (PSO). Therefore, in comparison to the GA or ACO algorithm, the SFLA has better global and local search capabilities. Figure 4 shows the process optimization flowchart using the SFLA; the right side shows the SFLA optimization process and involved parameters.
Figure 4.
SFLA-based stressing model methodology for parameter optimization.
The procedures are presented as follows. Based on the stressing model, the mechanism of energy transfer and dissipation in the WSMM is determined. Subsequently, the objectives and constraints for process optimization are proposed. The SFLA is employed for multi-objective optimization. The SFLA is designed as a meta-heuristic algorithm for seeking a solution to a combinatorial optimization problem by using a fitness function. A virtual frog acts as the host of the optimized parameter set , where each parameter is treated as a meme for cultural evolution. First, the virtual frog population is randomly generated within the constraints. Each frog has a fitness value that measures the goodness of the individual. The virtual frog population is partitioned into several memeplexes, and roulette is used to construct sub-memeplexes. Secondly, the worst frog in the sub-memeplexes is improved by the best frog in the sub-memeplexes and the global optimal frog, which completes the local search and global information exchange processes. The convergence criteria are met if one frog carries the “best memetic pattern so far” for fifteen consecutive instances. Finally, the optimized parameters are verified by a wet grinding test to further optimize the actual process.
3. Results
In order to illustrate the proposed parameter optimization approach on the WSMM system, two case studies, one for vertical wet grinding and the other for horizontal wet grinding, were developed.
3.1. Application on Pin-Type Vertical Stirred Mill
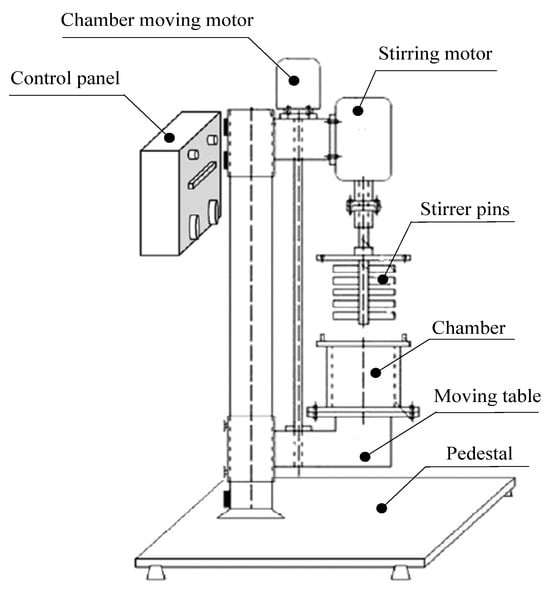
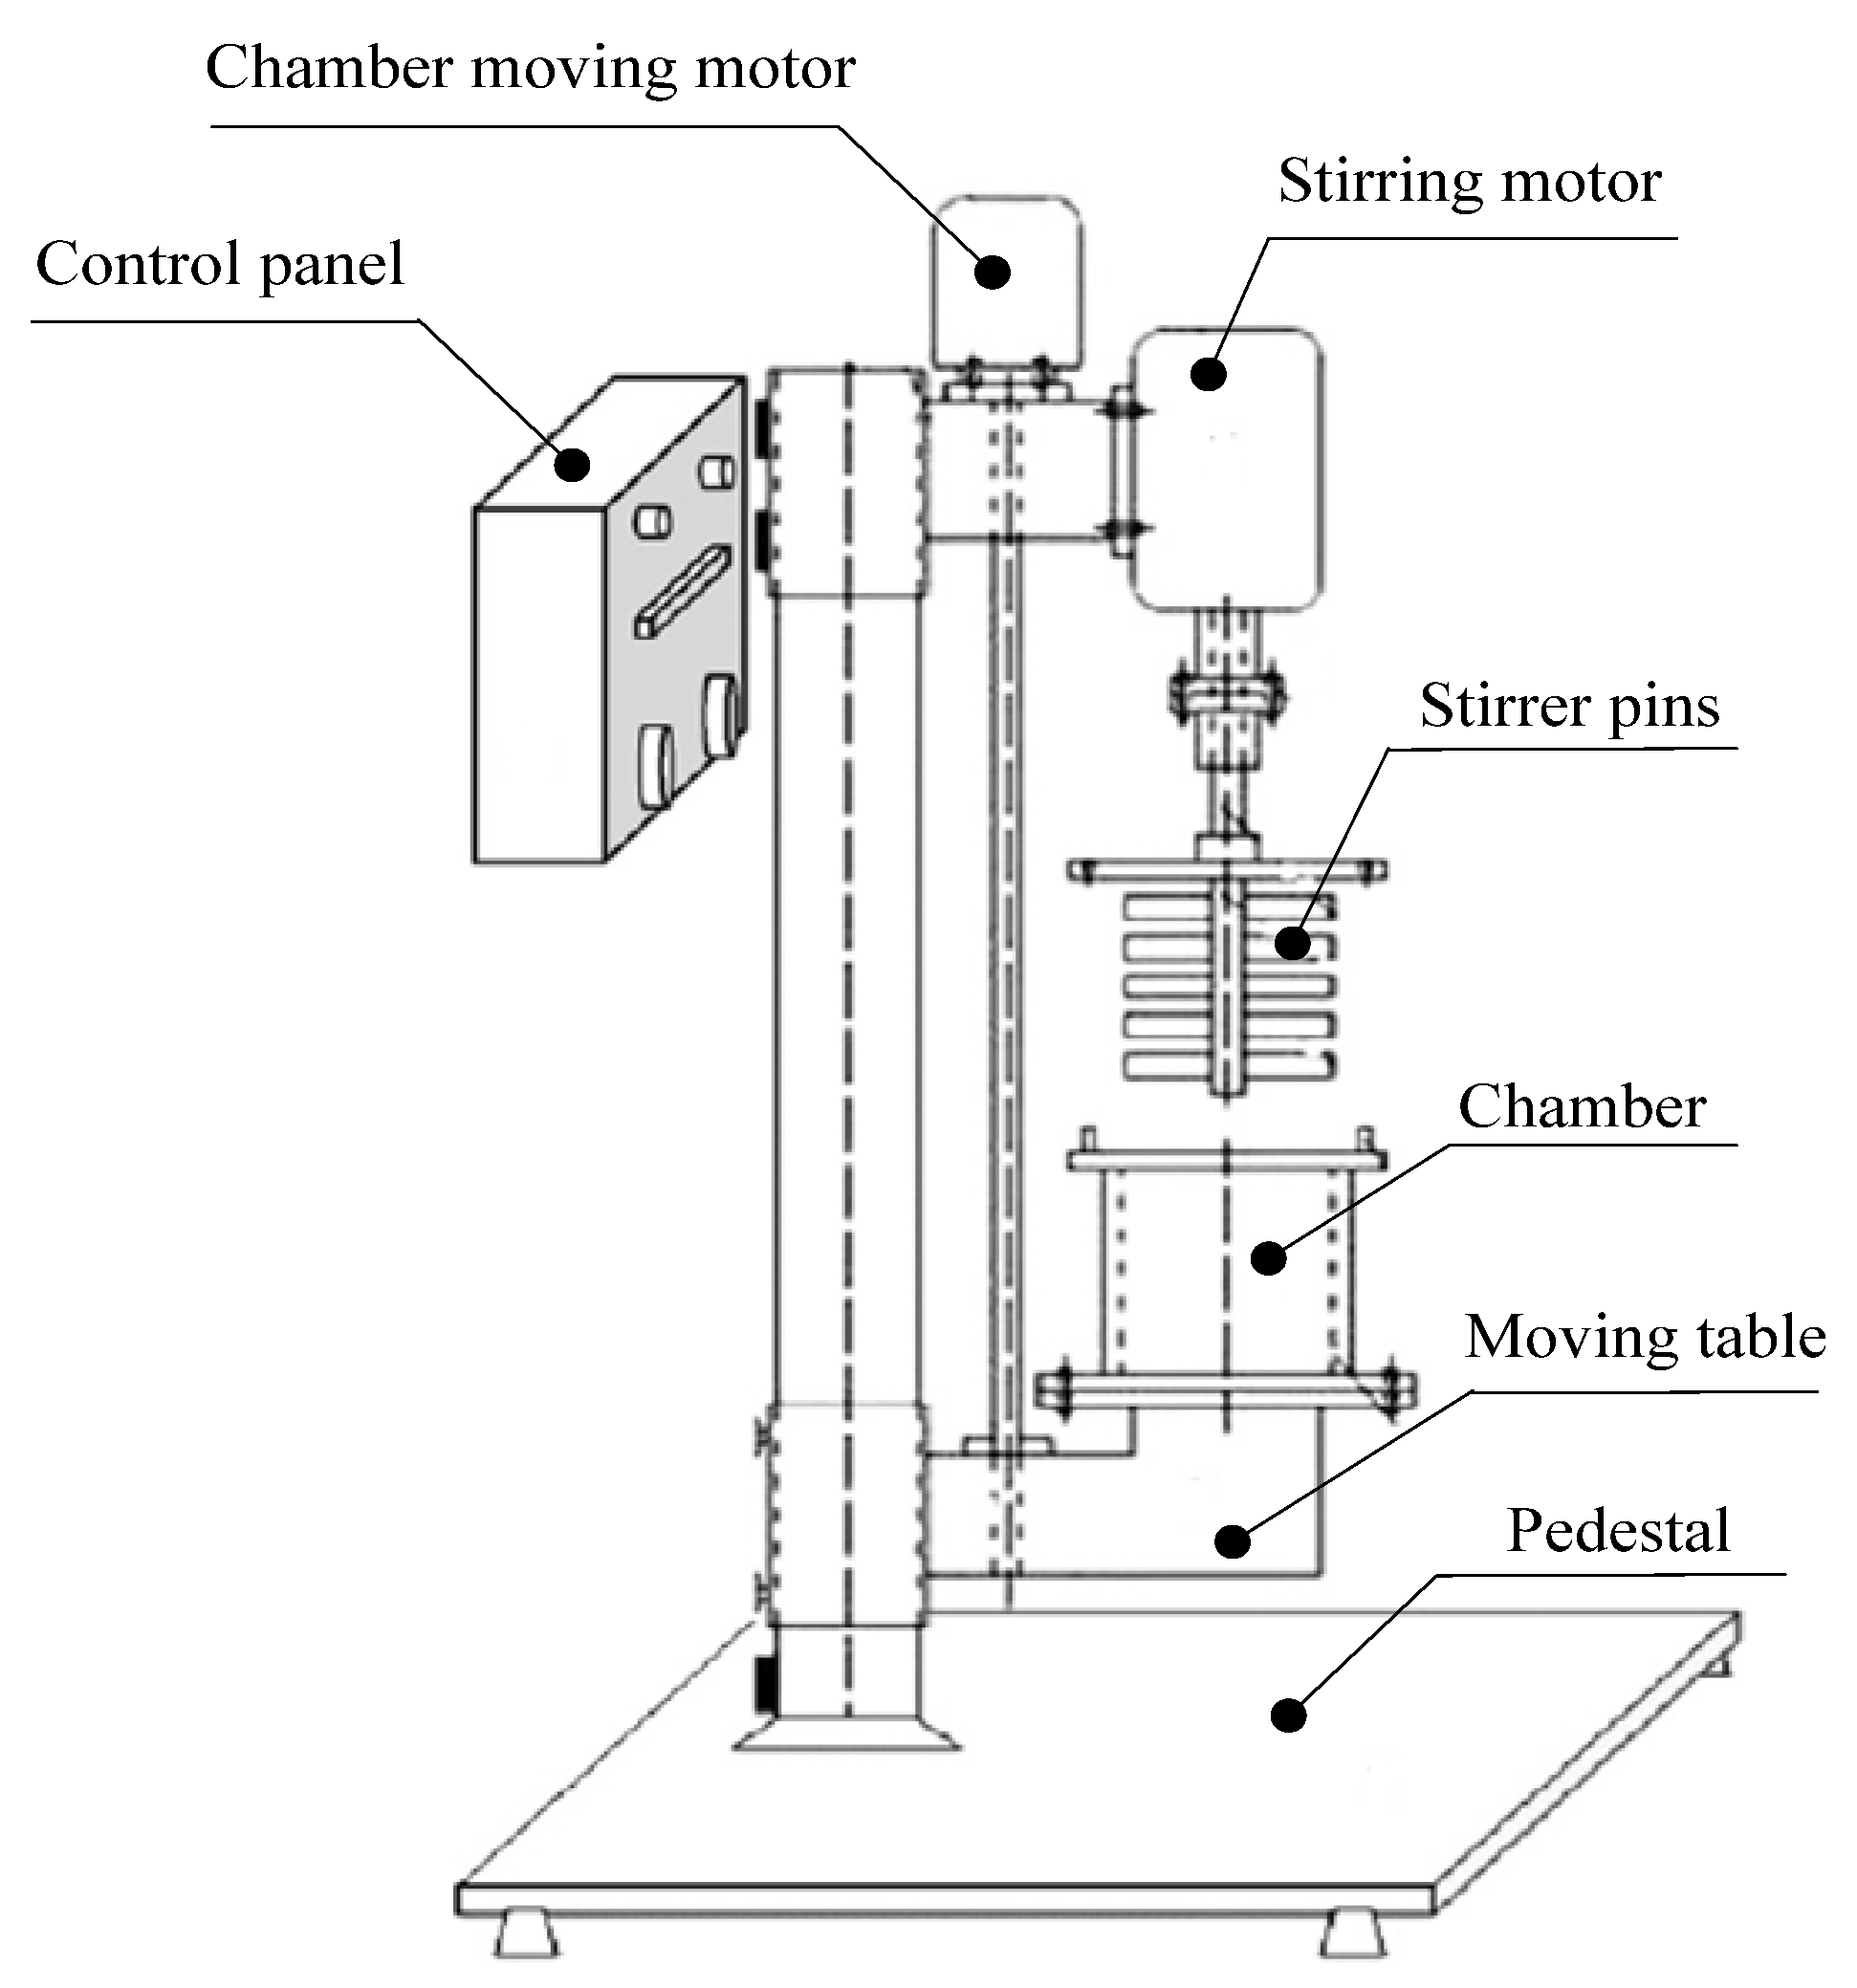
An antimonial refractory gold/silver ore sample was used as a grinding material. The material pretreatment and its material characteristics are described in Section 2.1. Grinding tests were carried out in a pin-type vertical stirred mill (Figure 5).
Figure 5.
Stirred media mill [9].
The stirrer consisted of 14 pins fitted to a shaft (Ø8.9 mm diameter). The chamber volume was 580 cm3, and the pulp density was maintained at 35% w/w during the grinding process. Three stirrer speeds were used: 250, 500, and 750 rpm. The grinding medium was stainless steel beads with an average density of 7.68 g/cm3 and three diameters (1, 3, 5 mm). The bead load was controlled at three charge ratios (60, 70, 80%). The coded level of the ball diameter (v1), stirrer speed (v2), and ball charge ratio (v3) can be obtained using the following formula:
The coded values and actual values in each run are listed on the left side of Table 4. The particle size was determined using a Malvern Mastersizer 2000 (Malvern Panalytical, Malvern, Worcestershire, UK), with the mean of five replicates recorded.
Table 4.
Grinding process parameters and predicted results as a reference benchmark [9].
The second-order model representing P80 was expressed as a function of the ball diameter (v1), stirrer speed (v2), and ball charge ratio (v3) for coded units based on the experimental data. To compare the effects of process optimization, we set the grinding time tg = 10 min. Then, the equation can be expressed as [9].
Table 4 shows the measured and predicted values of the product particle diameter P80. Each run was performed in duplicate, and their mean values were calculated. The predicted values were obtained from Equation (18). Using the data in Table 4, the mean relative error of the predicted values () was found to be 0.048, which indicates that Equation (18) is reliable and has a high predictive accuracy.
As illustrated in Equation (16), the process optimization had the multiple objectives of stress number (primary) and stress intensity (secondary) under the constraints of particle diameter and grinding time . This is because, in micro- and nano-material grinding, the main mechanism of particle crushing is shear and friction between grinding media, rather than normal impact [32]. Equation (16) was optimized using SFLA to minimize P80 within the experimental range. The SFLA algorithm was implemented in the mathematical software package (MATLAB 2022b). The SFLA parameters were set as follows: number of memeplexes m = 30, number of frogs in each memeplex n = 50, number of evolved individuals selected from each memeplex q = 50, local iteration number within each memeplex Lmax = 30, and maximum step size to be adopted by a frog after being infected Smax = 1. To facilitate industrial applications, the “actual levels” in Table 4 were employed as the optimized process parameters. The optimal levels of the variables were found to be the ball diameter = 1 mm, ball charge ratio = 80%, and stirrer speed = 750 rpm, with a prediction of P80 = 2.88 μm. In comparison to the actual levels listed in Table 4, the optimized process parameters can achieve the minimum product particle size within the grinding time.
3.2. Application on Pin-Type Horizontal Stirred Mill
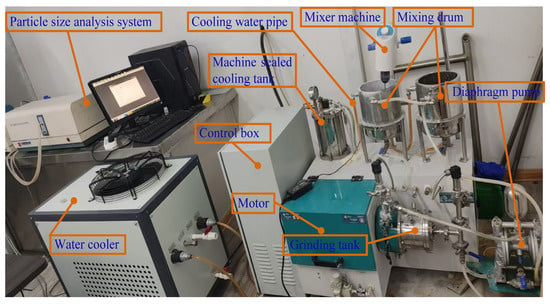
Heavy calcium carbonate (HCC) is used as an experimental material. The material pretreatment and its material characteristics are described in Section 2.1. Ultra-fine grinding tests are carried out in a batch scale pin-type horizontal stirred mill (RTSM-05) provided by Anhui Root Intelligent Equipment Co., Ltd. (Suzhou City, Anhui Province, China) (Figure 6). The stirred mill is comprised mainly of a grinding chamber, stirrer, motor, control box, diaphragm pump, and water cooler. The grinding chamber, which is jacketed for cooling water circulation, has a volume of 0.5 L. The maximum power of the motor is 4 kW, and the stirrer speed can be varied from 600 to 1300 rpm. The yttrium-stabilized zirconia beads, whose average density is 6.07 g/cm3 with a size of dgm = 0.30 mm, are used as grinding medium. The bead load for all the tests is fixed at 60% of the net mill volume. The product size distribution analysis was carried out by the laser diffraction method using a BT-2003 provided by Dandong Better size Instrument Co., Ltd. (Dandong City, Liaoning Province, China), which is China’s No. 1 player in the particle sizing business. Each particle size analysis was performed in three replicates, and the mean is presented in the results.
Figure 6.
Isometric view of RTSM-05 horizontal stirred mill.
A total of 50 experiments, in which the process parameters were provided and validated by company technicians, were conducted to assess the effect of the stirrer speed (nsr), grinding time (tg), initial product particle size (xp), and solids concentration (Cv) on the product particle size (P50). The range of the variables and the observed product size (P50) considered in this work are listed in Table 5.
Table 5.
Grinding process parameters and the observed product size (P50).
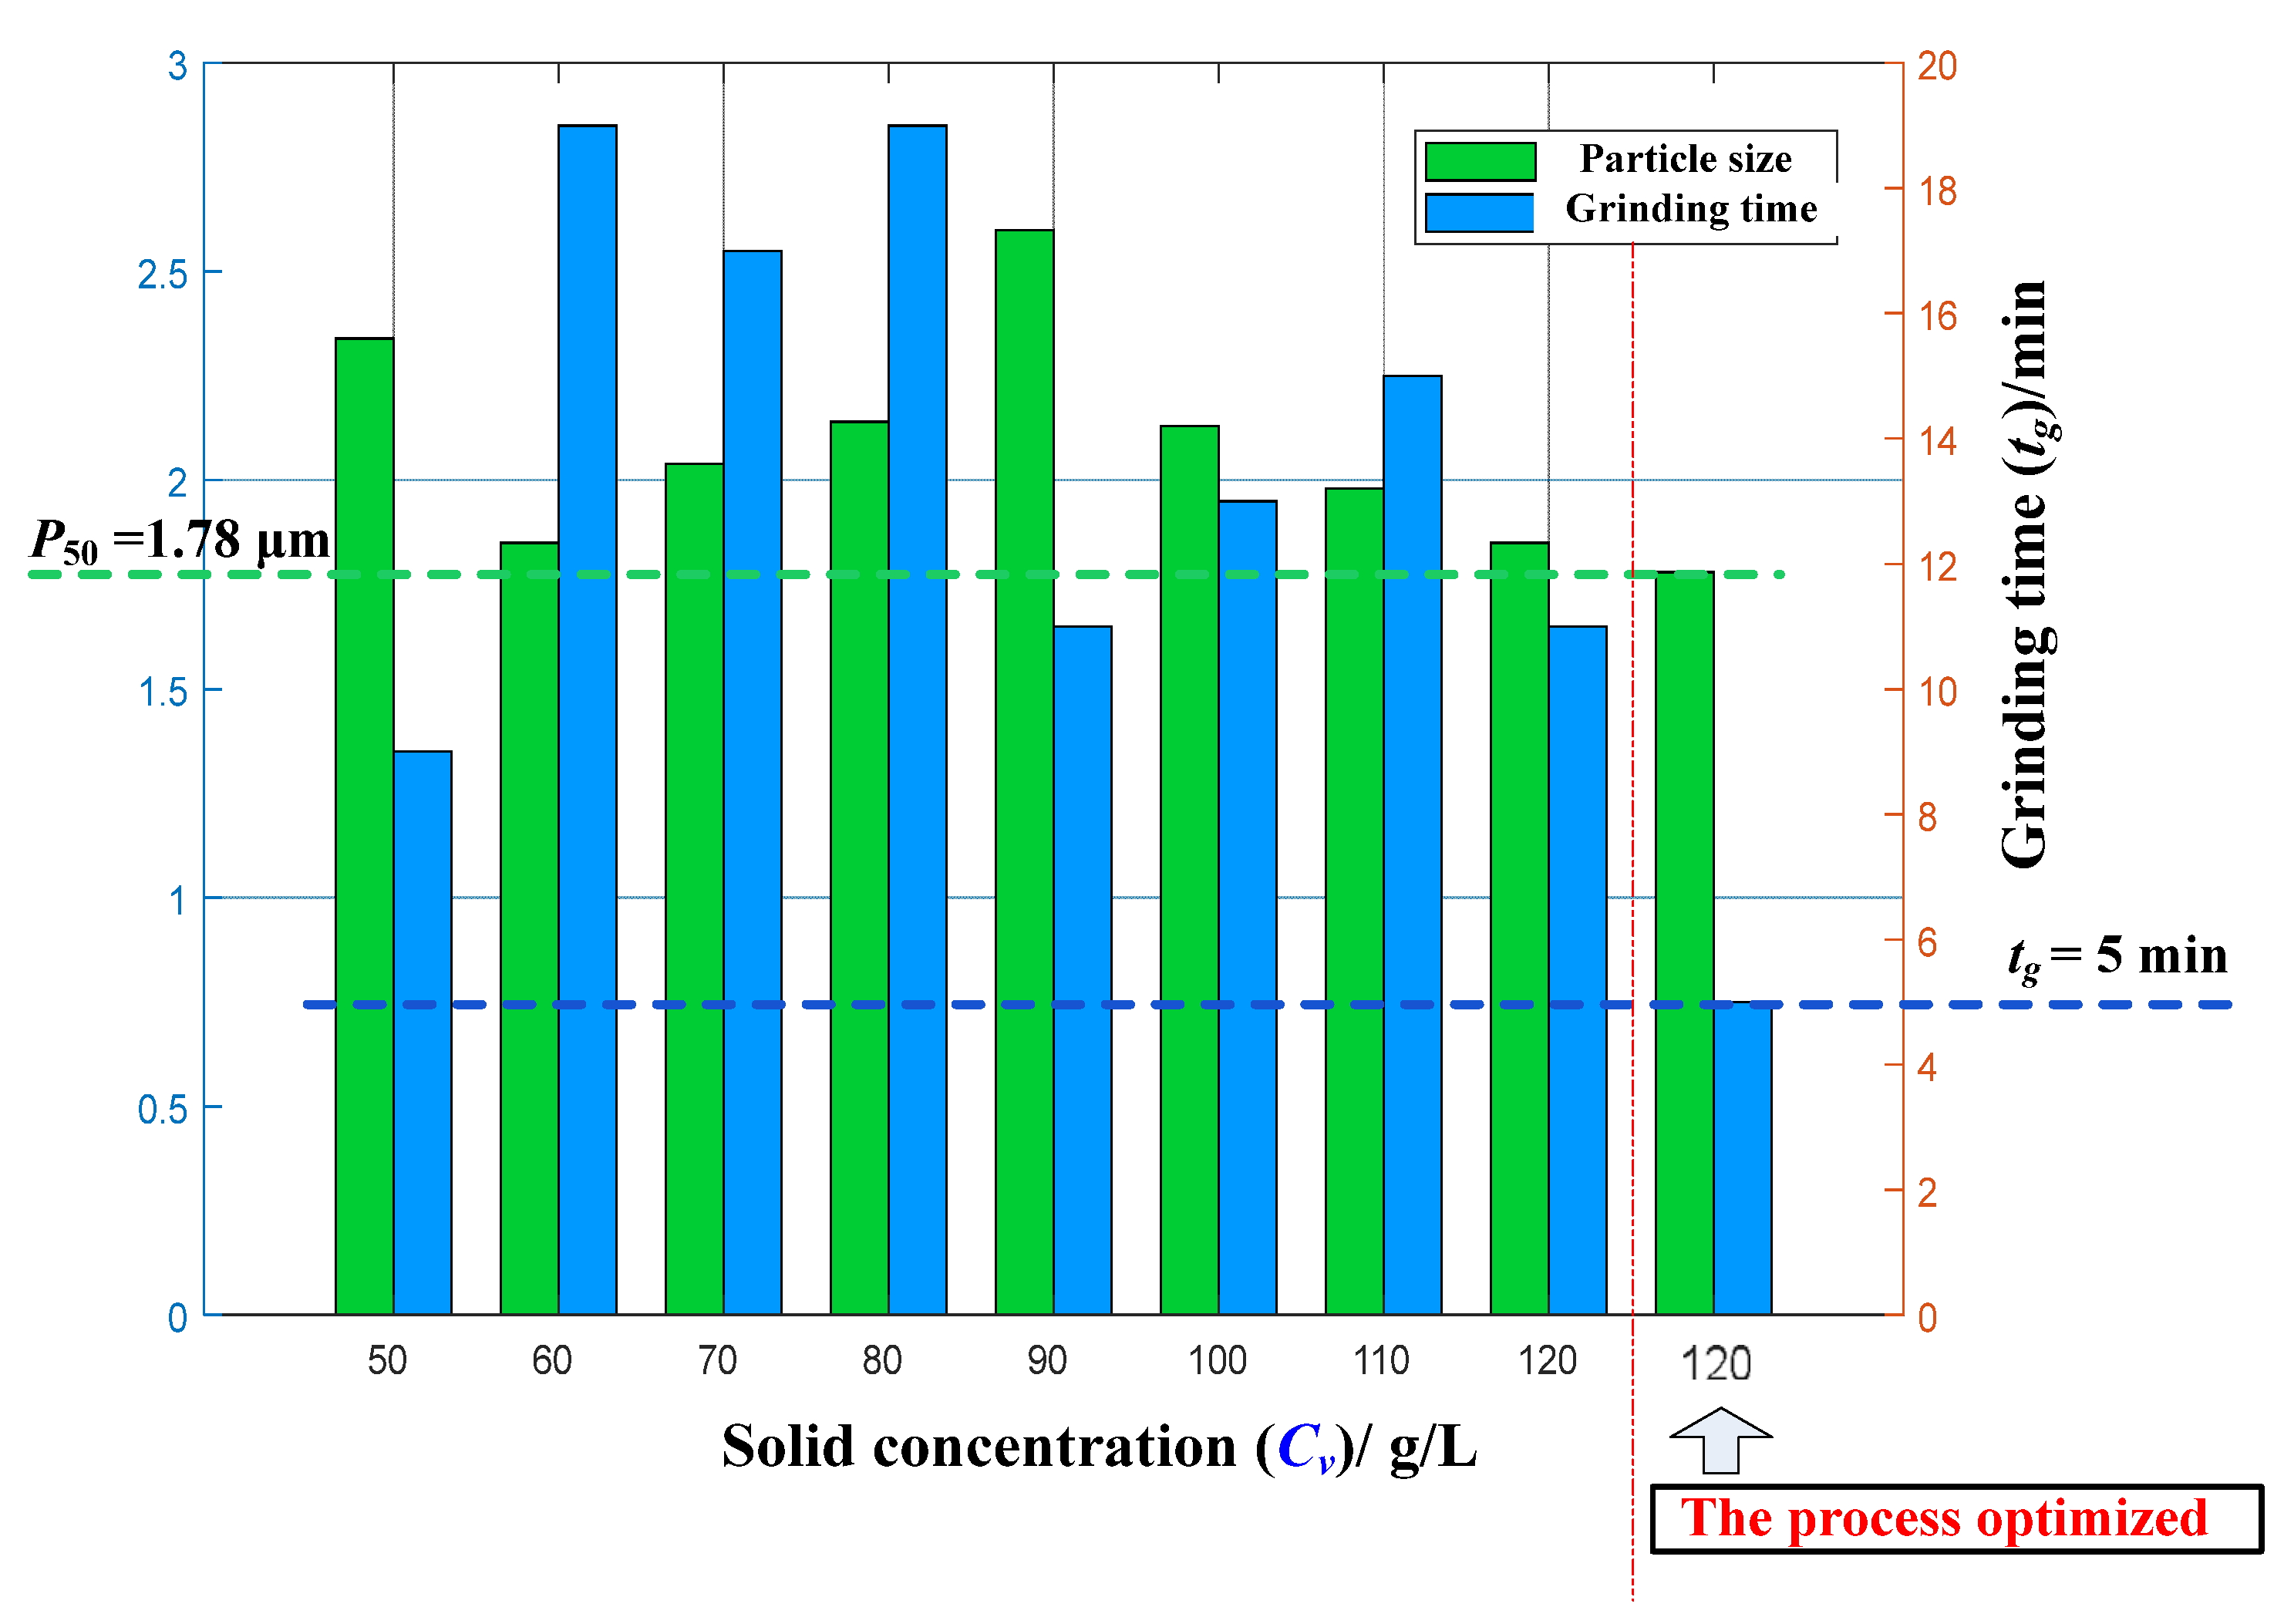
SFLA-based stressing model methodology is employed to acquire the optimal process parameters. In order to ensure the product productivity, the solids concentration, Cv, should be ensured to take the maximum value. The SFLA algorithm was implemented in the mathematical software package (MATLAB 2022b), with the following parameters: number of memeplexes m =30, number of frogs in each memeplex n =45, number of evolved individuals selected from each memeplex q = 30, local iteration number within each memeplex Lmax = 25, and maximum step size to be adopted by a frog after being infected Smax = 1. The optimal levels of the variables were found to be the stirrer speed nsr =1300 rpm, initial product particle size xp = 6 μm, and solid concentration of product particles Cv = 120 g/L. Ultra-fine grinding tests are reconducted in a RTSM-05 horizontal stirred mill using the process parameters optimized mentioned above. The results revealed that, after only tg = 5 min of grinding, the product particle size P50 is 1.78 μm. Figure 7 shows the product particle size under different wet milling process parameters. Focusing on the wet milling efficiency, the preferred milling processes parameters at different concentrations, shown in Table 5, were screened for comparative analysis to simplify the amount of data for comparison. As can be seen in Figure 7, the optimized process parameters can achieve the minimum product particle size (P50 = 1.78 μm) and maximum solid concentration (Cv = 120 g/L) within the minimum grinding time (tg = 5 min).
Figure 7.
Comparative analysis under different process parameters.
4. Conclusions
The parameter optimization of WSMM to achieve ultrafine grinding with improved milling capability and quality is crucial. The objective of this paper was to develop a parameter optimization methodology for multiple-objective WSMM optimization. A mechanistic model was proposed, and the specific energy was quantified according to a stressing model. To improve the single-particle comminution rate, the specific stress intensity and specific stress number were proposed. The objective of parameter optimization is to achieve the maximum specific stress intensity and specific stress number under the constraint of the product particle size. The SFLA was applied to find the optimal parameters. The performance of the proposed strategy is validated using two case studies in different industrial optimization scenarios. The result of the first case study illustrates that, in comparison to a quadratic programming-based response surface methodology, the proposed SFLA-based stressing model greatly enhances the wet grinding efficiency (decreasing P80 from 3.28 μm to 2.88 μm). In the second case study, the parameter optimization under different feed particle sizes and different productivities was discussed. The results confirmed that the optimized parameters can achieve the minimum particle size (P50 = 1.78 μm) and maximum solid concentration (Cv = 120 g/L) within the minimum grinding time (tg = 5 min). Notably, the core value of this study extends beyond laboratory validation, providing critical guidance for industries utilizing stirred media mills. The RTSM-05 horizontal stirred mill used in Case 2 is an industrial-grade device, consistent with commonly used equipment in the industry, and its optimization results can directly serve as a parameter reference for similar industrial equipment. In industrial scenarios, determining processes for new materials typically requires repeated high-cost pilot tests; however, this model can quickly predict optimal processes using only laboratory-scale material property data and mill parameters, significantly reducing trial-and-error costs and shortening process development cycles. Meanwhile, the model’s adaptability to different mill types (vertical and horizontal) provides a theoretical basis for enterprise mill selection—when enterprises need to switch between ore grinding (vertical mills) and chemical filler grinding (horizontal mills), the model can quickly match suitable parameters based on mill structure and material characteristics, avoiding the inefficiency of “one test per machine”.
Furthermore, through collaboration with Anhui Root Intelligent Equipment Co., Ltd. (Suzhou City, Anhui Province, China), the optimization strategy proposed has initially demonstrated advantages in preliminary industrial applications: in the grinding production of materials such as HCC, it not only achieves precise control of product particle size but also improves production stability, providing a scalable theoretical framework for the optimal design and efficient operation of industrial-grade stirred media mills.
In summary, the “SFLA-stressing model” system constructed in this study effectively bridges the gap between academic modeling and industrial application. It provides a practical cost-effective tool for industries using stirred media mills to improve production efficiency and reduce energy consumption and costs, and it holds broad prospects for industrial application. The proposed approach is systematic and robust and can be integrated into WSMM architectures for parameter optimization in other complex WSMM.
Author Contributions
Conceptualization, B.W. and K.H.; methodology, K.H. and F.S.; software and data curation, F.S.; investigation, X.L. and B.W.; draft preparation, K.H. and B.W.; funding acquisition, C.X. All authors have read and agreed to the published version of the manuscript.
Funding
This research was funded in part by the Natural Science Foundation of Anhui Province, grant number 2108085ME172; in part by the Suzhou University key project, grant numbers 2023yzd12; in part by Suzhou University Science and Technology Teachers to Enterprises Temporary Practice Plan Project, grant numbers 2024jsqygz115; in part by the Suzhou University School-enterprise cooperation practice education base project, grant number szxy2023xxhz06; in part by the Natural Science Research Project of Anhui Educational Committee, grant number 2023AH052235; in part by the Suzhou University Scientific Research Project, grant number 2023fzjj03; in part by the Suzhou Science and Technology Plan Project, grant number SZKJXM202411; and in part by the Intelligent Equipment Quality and Reliability Key Laboratory of Anhui Province Open Projects, grant numbers IEQRKL2405, IEQRKL 2406, IEQRKL 2407.
Data Availability Statement
The original contributions presented in this study are included in the article. Further inquiries can be directed to the corresponding author.
Acknowledgments
This work was carried out in Wet Grinding School-Enterprise Joint Laboratory of Suzhou University–Anhui Root Intelligent Equipment Co., Ltd. We sincerely thank Chengcai Xi for his technical support throughout the work.
Conflicts of Interest
Author Chengcai Xi was employed by the company Anhui Root Intelligent Equipment Co., Ltd. The remaining authors declare that the research was conducted in the absence of any commercial or financial relationships that could be construed as a potential conflict of interest.
References
- Altun, O.; Toprak, A.; Altun, D.; Altun, D.; Bilgili, E. Assessment of different energy-based breakage distribution functions in population balance model of an industrial scale continuously operated wet stirred media mill. Miner. Eng. 2024, 218, 109054. [Google Scholar] [CrossRef] [Scilit]
- Siewert, C.; Moog, R.; Alex, R.; Kretzer, P.; Rothenhäusler, B. Process and scaling parameters for wet media milling in early phase drug development: A knowledge based approach. Eur. J. Pharm. Sci. 2018, 115, 126–131. [Google Scholar] [CrossRef] [Scilit]
- Guo, W.; Gao, P.; Tang, Z.; Han, Y.; Meng, X. Effect of grinding media properties and stirrer tip speed on the grinding efficiency of a stirred mill. Powder Technol. 2021, 382, 556–565. [Google Scholar] [CrossRef] [Scilit]
- Flach, F.; Breitung-Faes, S.; Kwade, A. Model based process optimization of nanosuspension preparation via wet stirred media milling. Powder Technol. 2018, 331, 146–154. [Google Scholar] [CrossRef] [Scilit]
- Kwade, A. A stressing model for the description and optimization of grinding processes. Chem. Eng. Technol. Ind. Chem.-Plant Equip.-Process Eng.-Biotechnol. 2003, 26, 199–205. [Google Scholar] [CrossRef] [Scilit]
- Kwade, A. Mill selection and process optimization using a physical grinding model. Int. J. Miner. Process. 2004, 74, S93–S101. [Google Scholar] [CrossRef] [Scilit]
- Alamprese, C.; Datei, L.; Semeraro, Q. Optimization of processing parameters of a ball mill refiner for chocolate. J. Food Eng. 2007, 83, 629–636. [Google Scholar] [CrossRef] [Scilit]
- Hou, T.H.; Su, C.H.; Liu, W.L. Parameters optimization of a nano-particle wet milling process using the Taguchi method, response surface method and genetic algorithm. Powder Technol. 2007, 173, 153–162. [Google Scholar] [CrossRef] [Scilit]
- Celep, O.; Aslan, N.; Alp, İ.; Taşdemir, G. Optimization of some parameters of stirred mill for ultra-fine grinding of refractory Au/Ag ores. Powder Technol. 2011, 208, 121–127. [Google Scholar] [CrossRef] [Scilit]
- Mäntynen, A.; Zakharov, A.; Jämsä-Jounela, S.L.; Graeffe, M. Optimization of grinding parameters in the production of colorant paste. Powder Technol. 2012, 217, 216–222. [Google Scholar] [CrossRef] [Scilit]
- Breitung-Faes, S.; Kwade, A. Use of an enhanced stress model for the optimization of wet stirred media milling processes. Chem. Eng. Technol. 2014, 37, 819–826. [Google Scholar] [CrossRef] [Scilit]
- Montalescot, V.; Rinaldi, T.; Touchard, R.; Jubeau, S.; Frappart, M.; Jaouen, P.; Bourseau, P.; Marchal, L. Optimization of bead milling parameters for the cell disruption of microalgae: Process modeling and application to Porphyridium cruentum and Nannochloropsis oculata. Bioresour. Technol. 2015, 196, 339–346. [Google Scholar] [CrossRef] [Scilit]
- Nekkanti, V.; Marwah, A.; Pillai, R. Media milling process optimization for manufacture of drug nanoparticles using design of experiments (DOE). Drug Dev. Ind. Pharm. 2015, 41, 124–130. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Brunaugh, A.; Smyth, H. Process optimization and particle engineering of micronized drug powders via milling. Drug Deliv. Transl. Res. 2018, 8, 1740–1750. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Katircioglu-Bayel, D. Impact of operating parameters on the breakage process of talc. Min. Metall. Explor. 2020, 37, 1717–1727. [Google Scholar] [CrossRef] [Scilit]
- Santosh, T.; Soni, R.K.; Eswaraiah, C.; Rao, D.; Venugopal, R. Optimization of stirred mill parameters for fine grinding of PGE bearing chromite ore. Part. Sci. Technol. 2020, 39, 663–675. [Google Scholar] [CrossRef] [Scilit]
- Katircioglu-Bayel, D. Optimization of operating parameters on dry grinding of calcite in a stirred media mill using the Box-Behnken design. Minerals 2020, 10, 251. [Google Scholar] [CrossRef] [Scilit]
- Amini, R.K.; Kitamura, Y.; Islam, M.Z.; Kokawa, M.; Eseese, V.F. Impact of micro wet milling process on pomegranate peel phenolics extraction using multi-response optimization. J. Food Meas. Charact. 2021, 15, 2865–2876. [Google Scholar] [CrossRef] [Scilit]
- Guner, G.; Mehaj, M.; Seetharaman, N.; Elashri, S.; Yao, H.F.; Clancy, D.J.; Bilgili, E. Do mixtures of beads with different sizes improve wet stirred media milling of drug suspensions? Pharmaceutics 2023, 15, 2213. [Google Scholar] [CrossRef] [Scilit]
- Wang, Z.; Hou, Y.; Sobhy, A. Prediction and optimization of tower mill grinding power consumption based on GA-BP neural network. Physicochem. Probl. Miner. Process. 2023, 59, 172096. [Google Scholar] [CrossRef] [Scilit]
- BAHETI, V.; ABBASI, R.; MILITKY, J. Optimisation of ball milling parameters for refinement of waste jute fibres to nano/micro scale in dry conditions. J. Text. Eng. 2013, 59, 87–92. [Google Scholar] [CrossRef] [Scilit]
- Gbadeyan, O.J.; Sithole, B.; Adali, S.; Bright, G. Process optimization of nano-calcium carbonate produced from snail shell using supermasscollider. Part. Sci. Technol. 2024, 42, 659–667. [Google Scholar] [CrossRef] [Scilit]
- Guo, K.; Chen, H.; Liu, Q.; Guo, W.; Li, Y.; Xing, Y.; Gui, X. Optimizing the process parameters in stirred-media mills using mathematical modeling. Part. Sci. Technol. 2025, 43, 217–228. [Google Scholar] [CrossRef] [Scilit]
- Bilgili, E.; Guner, G. Mechanistic modeling of wet stirred media milling for production of drug nanosuspensions. AAPS PharmSciTech 2020, 22, 2. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Coello, C.C. Evolutionary multi-objective optimization: A historical view of the field. IEEE Comput. Intell. Mag. 2006, 1, 28–36. [Google Scholar] [CrossRef] [Scilit]
- Romeis, S.; Schmidt, J.; Peukert, W. Mechanochemical aspects in wet stirred media milling. Int. J. Miner. Process. 2016, 156, 24–31. [Google Scholar] [CrossRef] [Scilit]
- Becker, M.; Kwade, A.; Schwedes, J. Stress intensity in stirred media mills and its effect on specific energy requirement. Int. J. Miner. Process. 2001, 61, 189–208. [Google Scholar] [CrossRef] [Scilit]
- Kwade, A.; Schwedes, J. Breaking characteristics of different materials and their effect on stress intensity and stress number in stirred media mills. Powder Technol. 2002, 122, 109–121. [Google Scholar] [CrossRef] [Scilit]
- Kwade, A. Determination of the most important grinding mechanism in stirred media mills by calculating stress intensity and stress number. Powder Technol. 1999, 105, 382–388. [Google Scholar] [CrossRef] [Scilit]
- Zohrehvandi, M.; Zohrehvandi, S.; Khalilzadeh, M.; Amiri, M.; Jolai, F.; Zavadskas, E.K.; Antucheviciene, J. A multi-objective mathematical programming model for project-scheduling optimization considering customer satisfaction in construction projects. Mathematics 2024, 12, 211. [Google Scholar] [CrossRef] [Scilit]
- Pereira, J.L.J.; Oliver, G.A.; Francisco, M.B.; Cunha Jr, S.S.; Gomes, G.F. A review of multi-objective optimization: Methods and algorithms in mechanical engineering problems. Arch. Comput. Methods Eng. 2022, 29, 2285–2308. [Google Scholar] [CrossRef] [Scilit]
- He, K.; Jia, M.; Sun, F.; Yang, Q.; Wu, B.; Li, X.; Meng, C. Simulation of grinding media motion and collisions in wet-operated accelerator-mill using DEM coupled with CFD. Minerals 2022, 12, 341. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2025 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license (https://creativecommons.org/licenses/by/4.0/).