


Abstract
This study investigated the effect of ozonation of wheat flour (30 ppm O3 for 30 min) on the microbiological status of flour, as well as the profile of volatile compounds, the mechanical properties, and the sensory characteristics of the resulting bakery products. Ozonation significantly reduced the microbial load of the flour, decreasing aerobic bacteria from 1.4 × 10⁵ to 1.7 × 10⁴ CFU·g−1 and yeasts and moulds from 2.8 × 10³ to 1.3 × 10² CFU·g−1, while lactic acid bacteria populations remained unchanged. HS-SPME-GC-MS analysis revealed that the ozonated flour contained six volatile compounds (compared to three in the control), predominantly nonanal (80.62%), an aldehyde formed via the ozonolysis of unsaturated fatty acids. Although these ozone-induced aldehydes were also detected in the final bakery products, their peak areas decreased substantially (to ≤3.3% of the flour values), suggesting thermal desorption during baking. Texture profile analysis demonstrated that products baked from ozonated flour exhibited increased hardness (Cycle 1: 68.06 N vs. 53.42 N; Cycle 2: 59.41 N vs. 47.52 N) and chewiness (427.95 mJ vs. 404.70 mJ) compared to controls. This textural degradation is likely due to ozone-induced modifications in enzyme activity (proteolytic, amylolytic, and lipolytic) and gluten protein cross-linking via disulphide bond formation. Furthermore, sensory evaluation using a five-point scale showed lower acceptability for the ozonated products (3.04 vs. 3.74), with panellists noting inferior taste, aroma, crumb colour, and flexibility. In conclusion, while ozonation effectively reduces the microbiological load of wheat flour, the applied high-dose treatment (30 ppm, 30 min) negatively impacts the sensory and textural quality of the bakery products, indicating that milder processing parameters are necessary to balance safety and quality.
Keywords:
ozone; flour; microbiological load; bakery; volatile compounds; nonanal; analysis of texture profile 1. Introduction
Wheat flour is a valuable element of the human diet. Some of the elements that are important from the perspective of healthy nutrition are nutritional fibre, protein, minerals, and vitamins of group B. It is rich in starch consisting of amylase and amylopectin, and it contains small amounts of lipids [1]. Flour can undergo various modifications with the aim of improving the final quality of bakery products. Modifications include the addition of a number of emulsifiers, oxidants, enzyme preparations, and organic acids, whose addition may negatively impact the final quality of bread or other bakery products [2].
Ozone is a very potent oxidant that possesses strong antimicrobial properties. This agent in its gaseous form or incorporated into a water solution is widely used for preservation purposes [3]. Ozone treatment was verified as a method to reduce microorganisms such as bacteria and fungi and and/or their seven metabolites, such as mycotoxins. This can be exploited to reduce the risk of acute and chronic toxicity due to mycotoxins in matrices such as wheat or maize and the flour obtained from them. Importantly, numerous studies indicate that ozonation can significantly reduce the microbial load in cereal-based matrices, including flour, by inactivating a wide spectrum of spoilage and pathogenic microorganisms. The effectiveness of this process depends on factors such as ozone concentration, exposure time, moisture content, and the physical structure of the treated material. As a result, ozonation is increasingly considered a promising non-thermal decontamination method that enables the improvement of microbiological safety without the need for chemical preservatives or high-temperature processing [4,5,6,7,8,9]. Earlier research provided extensive data on the efficacy of ozone utilisation to reduce microbial activity in soft fruits, herbs, grains, or other plant matrices. In addition, it can be utilised to modify various elements of food products. What is more, ozone is recognised as a safe substance that can be used for treatment of food products [10]. The utilisation of ozone for the processing of flour may be an attractive alternative as an innovative means of improving the properties of the product, due to its oxidative action [11].
Additionally, ozone has been successfully applied in the cultivation and post-harvest handling of cereal crops such as wheat and maize. In agricultural practice, ozone treatment can be used to disinfect seeds, reduce pathogenic microorganisms in the rhizosphere, and improve plant resistance to fungal infections. In post-harvest processes, ozone can effectively reduce microbial contamination and degrade mycotoxins in stored grains, contributing to improved safety and quality of raw materials for milling and feed production. Its application in the processing of wheat and maize therefore represents a sustainable and environmentally friendly technology that improves both the safety of the product and its nutritional value [12].
In addition, particularly in the case of ozone treatment, it is important that food products characterised by a minimal degree of modification and free of chemicals utilised for conservation purposes become more and more desired by the consumer worldwide. This results in modifications of the means of preservation of food products.
However, this oxidant can also be a factor responsible for unwanted changes in the organoleptic and physicochemical properties of food products [13]. Other authors indicated a potential of application for ozone at the stage of wheat drying. During drying and ozonation of wheat, other authors observed that the content of proteins present in the wheat matrix is an index that is crucial in relation to the breadmaking procedures—which is reflected by the presence of gluten [14]. Moreover, it was reported that utilisation of ozone at a concentration of 75 ppm as reported by Wang et. al. [15] had no significant effect on the content of wheat protein after 90 min of ozonation. In general, wheat protein is composed of four main types: glutenin, gliadin, albumin, and globulin. Gliadin, albumin, and globulin, which are soluble polymeric flour proteins, did not show obvious changes when kernels were exposed to ozone for no more than two and a half minutes at the flow rate of 6 g/h [16].
The main obstacle to the wide utilisation of ozone in all possible food matrices is the possible complex effects on various constituents of food products. For instance, during the utilisation of this oxidant, undesired reactions with flour compounds such as lipids may occur, which as a consequence could change the properties of the final product in an undesired way. Other authors conducted whole maize flour ozonation. In the case of maize flour ozonation, which was conducted by Alexandre et al. [17], a decrease in the proportion of linoleic, oleic, and α -linolenic fatty acids was observed. Aside from the possibility that lipid oxidation by ozone can contribute to significant changes in the products’ aroma, ozone can also degrade a number of chemical compounds or modify their mechanical properties [18].
Therefore, to observe the potential complex effects of the impact of ozone on the exposed flour matrix, analyses of the fraction of volatile compounds and the mechanical properties of the bakery product were conducted. The purpose of the presented research was to determine the impact of the microbial status of wheat flour ozonation on the composition of volatile compounds isolated from treated products, as well as on the organoleptic properties and mechanical properties of the bakery product prepared from treated and control (non-ozonated) flour. Consequently, the specific objectives of this study were to (1) determine the effect of applied ozonation conditions on the improvement of the microbiological status of flour; (2) evaluate the effect of ozone treatment on the volatile compound composition of wheat flour and bakery products; (3) assess the influence of ozonation on the mechanical and textural properties of the bakery products obtained; and (4) determine the impact of flour ozonation on the sensory (organoleptic) quality of bakery products. The research hypothesis was that ozonation of wheat flour induces significant changes in its volatile compound composition, as well as in the mechanical and sensory properties of bakery products compared to non-ozonated flour.
2. Materials and Methods
2.1. Materials for the Preparation of Bakery Products
This study utilised wheat flour of the “Basia” brand, classified as type 405. A total of 6 kg of the material was purchased from a retail supermarket in Rzeszów, southern Poland. Upon inspection, the packaging was intact with no visible damage, and the flour showed no signs of contamination. The material was divided into six 1 kg samples. Three samples were subjected to the ozonation process, while the remaining three served as untreated controls.
2.2. Modification of Flour Parameters by Ozonation
Ozonation of wheat flour was carried out in a laboratory-scale reactor chamber with a total volume of 2 dm3. For each experiment, a 1 kg flour sample was evenly distributed as a thin layer inside the reactor to ensure uniform exposure to ozone and to facilitate efficient mass transfer. Ozone gas was generated using a “Korona L5 Zdrowa żywność” ozone generator (KoronaLab, Piotrków Trybunalski, Poland) and continuously supplied to the reactor at a flow rate of 18 dm3·min−1. These conditions enabled fluidisation of the flour particles, promoting homogeneous mixing and consistent contact between the gas phase and the material.
The ozonation process was conducted for 30 min at a constant ozone concentration of 30 ppm. The application of these contrasting conditions was intended to clearly demonstrate the potential impact of ozonation on the microbial status and technological properties of wheat flour and bakery products. Such an approach allowed for the identification of the maximum observable effects of the ozonation process and provided a basis for evaluating the practical significance of ozone treatment. The concentration of ozone was continuously monitored using a 2B Technologies 106 M ozone analyser (Boulder, CO, USA) to ensure process stability and repeatability.
All experiments were performed in triplicate under identical conditions.
2.3. Analysis of the Microbiological Load of Flour
The research material consisted of wheat flour subjected to ozone treatment and a control sample (not ozonated). Microbiological analyses were carried out in accordance with the methodology described by Matłok et al. [19]. The number of colony-forming units in the raw material was determined using the method specified in PN-ISO 15214:2002 (Polish Committee for Standardization, Warsaw, Poland, 2002) “Microbiology of food and animal feeding stuffs—Horizontal method for the enumeration of mesophilic lactic acid bacteria—Colony-count technique at 30 °C”. In accordance with this method, the count of living mesophilic lactic acid bacteria is performed in solid MRS medium incubated at a temperature of 30 °C for 72 h. The yeast and mould count in 1 g of material was determined using the method described in PN-EN ISO 21527-1:2009 “Microbiology of food and animal feeding stuffs—Horizontal method for the enumeration of yeasts and moulds. Colony count technique at 25 °C”. Enumeration of mesophilic aerobic bacteria in the relevant raw material was performed using the plate count method, in accordance with the standard set forth in (Ae) (O) PB-77/LM, 4th edition, dated 7 December 2015. The analyses were performed in triplicate.
2.4. Preparation of Model Bakery Product
A sample of 480 g of flour was placed in a vessel. In addition to the flour matrix, 4 g of salt, 4 g of sugar, 8 g of sodium bicarbonate, 250 mL of fermented milk product (kefir), and one egg were mixed together until a homogeneous mass was obtained. Based on this homogeneous mixture, the bakery products were formulated. The products had an ellipsoidal shape and were 1 cm in height. The prepared dough (baking mass) was placed in an oven preheated to 195 °C and baked for 15 min. The baked products were prepared from flour either modified with ozone gas (30 ppm 30 min) or not ozonated (control sample). The bakery products from the tested variants were baked in six replicates.
2.5. Analyses of Volatile Compounds by Means of HS-SPME
The modified and control flours and the prepared bakery products were subjected to analyses using the HS-SPME method in accordance with the Head Space–Solid Phase Microextraction (HS-SPME) methodology presented by Matłok et al. [19]. First, the raw materials were subjected to head space–solid phase microextraction analyses, with the use of 100 μm polydimethylsiloxanes (PDMS) fibre manufactured by Supelco Ltd. (Bellefonte, PA, USA). Prior to the analyses, the fibre was conditioned in accordance with the manufacturer’s instruction, at 250 °C for a duration of 30 min in the injector of a gas chromatograph. The refined material, with a weight of 3 ± 0.01 g, was placed in a 100 mL glass vial and sealed with a cap equipped with a silicone seal. Exposure of the fibre in the headspace phase of the samples took place for 30 s at a temperature of 20 °C. Subsequently, the fibre was transferred to the injector of the gas chromatograph (temperature 250 °C), where the analytes were thermally desorbed for a duration of 5 min. The composition of the compounds desorbed from SPME fibre was examined using a gas chromatograph (GC-MS, Varian 450GC coupled with 240 MS).
2.6. Chromatographic Analysis
The composition of volatile compounds that desorbed from the SPME fibre was investigated using GC-MS Varian 450 GC coupled with a mass detector Varian 240 MS system (SpectraLabScientific Inc., Markham, ON, Canada). The carrier gas, with a flow rate of 1 mL·min−1, was helium. The injector temperature was 250 °C. The separation of compounds was conducted using a capillary column (30 m × 0.25 mm) filled with a moderately polar stationary phase HP-5 with a layer thickness of 0.25 μm. The temperature program of the column oven was as follows. The program started at 50 °C for 5 min isotherm. Next, a temperature gradient of 10 °C/min up to 300 °C (5 min isotherm) was set up. The particular compounds were identified following the NIST.08 and Willey databases. The content of the components is given as the percentage area share of the analyte’s peak in the mixture. The chromatographic analysis was conducted in triplicate.
2.7. Analysis of Texture Profile of Bakery Products
In order to perform an instrumental texture profile analysis (TPA test) of the bakery products’ texture, a TextureProCT V1.2 Build 9 texture analyser from Brookfield Engineering Labs. Inc. (Middleboro, MA, USA) was utilised. The device was connected to a PC that in turn registered the chosen parameters of the texture of the investigated bakery products. To perform these measurements, a cuboid sample was cut from the bakery product (20 × 20 × 15 mm). The prepared samples were then placed under a flat pressure plate and subjected to a double compression test using the texture profile analysis test. The compression speed was set at 1 mm s−1, and the deformation level was standardized at 50% of the sample height to ensure uniform testing conditions. The texture analysis made it possible to determine the hardness, elasticity, and gumminess of the tested bread, all of which are force parameters. The texture profile analysis (TPA) was performed on bread crumb samples cut from the central part of the loaf into cubes with a height of approximately 15 mm. This dimension was chosen to ensure uniformity of the material and to minimize the influence of the crust on the texture measurements. Comparable sample heights have also been applied in previously published studies on bread texture (Wójcik et al., 2023; Foods, MDPI) [20] and in experimental protocols describing TPA analysis of bakery products (Bio-protocol, MDPI). Therefore, the selected sample size is considered methodologically acceptable and consistent with current research practice.
2.8. Sensory Evaluation of the Prepared Bakery Products from Ozonated and Control Flour
The sensory evaluation of the prepared bakery products based on the utilisation of ozonated and control flour was conducted according to a five-point method based on sensory evaluation cards. Sensory evaluation of the bakery products was conducted using a trained panel composed of 10 panellists selected based on their prior experience and ability to discriminate basic tastes and aromas, in accordance with ISO 8586:2012 guidelines for sensory panel selection. Prior to the evaluation, the panellists participated in a short calibration session to familiarise themselves with the evaluation criteria and scoring system. The samples were coded with random three-digit numbers and served in a randomised order to prevent bias. Each sample was presented individually on white, odourless plates under controlled lighting conditions to minimise visual influence. Serving temperature was standardised at 25 °C to ensure uniform sensory perception. The panellists were instructed to evaluate the samples based on a structured questionnaire assessing key sensory attributes such as shape and external appearance, colour of the rind, thickness of the crust, colour and appearance of the crumb, crumb porosity, elasticity of the crumb, and taste and smell of the bakery products, using a five-point hedonic scale (see Supplementary Materials). The sensory attributes were scored using a five-point hedonic scale, where 1 indicated the lowest quality/intensity, and 5 indicated the highest quality/intensity of the evaluated attribute. In accordance with the ISO methodology, weighted importance indicators were applied for each evaluated sensory attribute, as follows: shape and external appearance—0.2; colour of the rind—0.1; thickness of the rind—0.1; colour and appearance of the crumb—0.1; porosity of the crumb—0.1; flexibility of the crumb—0.1; and taste and smell—0.3. In accordance with the ISO methodology, appropriate importance indicators were applied when calculating the sensory evaluation results. Water and unsalted crackers were provided to cleanse the palate between samples. All sensory sessions were conducted in a dedicated sensory laboratory designed according to ISO 8589:2007 standards to minimise external distractions and ensure consistent testing conditions.
2.9. Statistical Analysis of the Results
The results were subjected to statistical analysis using STATISTICA 13.1 software (TIBCO Software Inc., Hillview Avenue, Palo Alto, CA, USA). Statistically significant differences between the parameters of bakery products prepared from ozonated and control flour were determined using Student’s t-test at a significance level of α = 0.05.
3. Results and Discussion
3.1. Analysis of the Microbiological Load of Flour
The ozone treatment of wheat flour conducted at a concentration of 30 ppm for 30 min significantly affected its microbiological load (Table 1). In the modified flour samples, a substantial reduction in the number of aerobic bacteria was observed, with the average level reaching 1.7 × 10⁴ CFU g−1 compared to 1.4 × 10⁵ CFU g−1 in the control samples, confirming the high effectiveness of ozone in reducing this group of microorganisms. A similar trend was observed for yeasts and moulds, whose average counts decreased from 2.8 × 10³ CFU g−1 to 1.3 × 10² CFU g−1, indicating a significant antifungal effect of the applied treatment. In contrast, the number of lactic acid bacteria in both variants was comparably low (<1.0 × 101 CFU g−1) and did not show significant differences, suggesting either limited sensitivity of this group of microorganisms to the applied ozonation conditions or their low initial presence in the tested material. The results clearly indicate that the application of ozone under the parameters used leads to a significant reduction in the overall microbiological load of wheat flour, which may contribute to improving its microbiological quality and the safety of the raw material.
Table 1.
Analysis of the microbiological load of flour as a function of the ozone dose applied.
The obtained results indicate that ozonation of wheat flour at a concentration of 30 ppm for 30 min leads to a significant reduction in the counts of aerobic bacteria as well as yeasts and moulds, confirming the strong antimicrobial properties of ozone. The mechanism of action of ozone involves the intensive oxidation of microbial cellular components, including membrane lipids, proteins, and genetic material, which results in cell inactivation and death [21]. The effectiveness of ozone has also been confirmed by Tiwari et al. [22], who demonstrated its ability to reduce the microbiological load in cereal products and plant-based raw materials. The lack of significant differences in the number of lactic acid bacteria may result from their greater resistance to oxidative stress, which is consistent with the observations reported by Guzel-Seydim et al. [23], who emphasised that microbial sensitivity to ozone depends on the cellular structure and the environment in which microorganisms occur. The results obtained confirm that ozonation is an effective method for reducing the microbial load of flour; however, its effect may vary depending on the type of microorganism and the conditions of the process.
3.2. Analysis of the Volatile Compounds Profile of Wheat Flour and Bakery Products with the HS-SPME Method
Wheat flour is a complex matrix consisting of a mixture of polysaccharides, proteins, and fats. Based on the research conducted to date, it was revealed that ozonation can modify proteins, especially enzymes, which are a significant group of compounds within wheat flour. In particular, amylolytic, proteolytic, and lipolytic enzymes may be affected [24]. Aside from protein compounds, lipids can also be severely affected by ozonation treatment. Especially fats with unsaturated bonds may be affected, as a result of ozonolysis of double bonds. This in turn leads to generation of lipid degradation products such as carbonyl compounds, such as aldehydes and ketones. In the case of oxidation of unsaturated lipids, aldehydes are often generated. Their construction depends mainly on the length of the carbon chain of the fatty acid to be decomposed [25].
This process may result in the generation of volatile compounds that can directly modify the organoleptic properties of the treated matrix. To indicate the possible impact of the flour ozonation process on product properties, several HS-SPME analyses were carried out. The bakery products were analysed in the same manner as the flour samples.
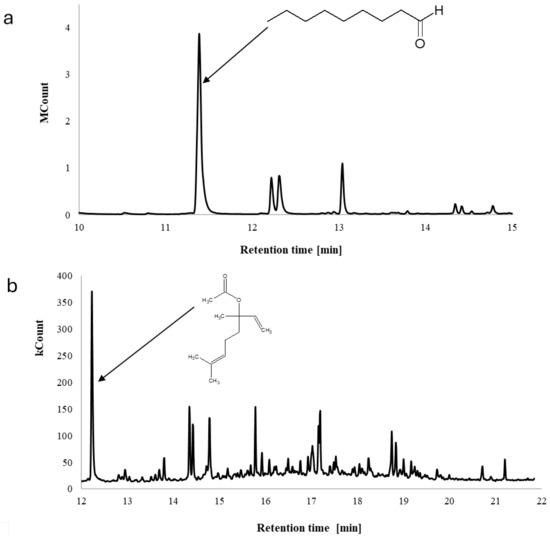
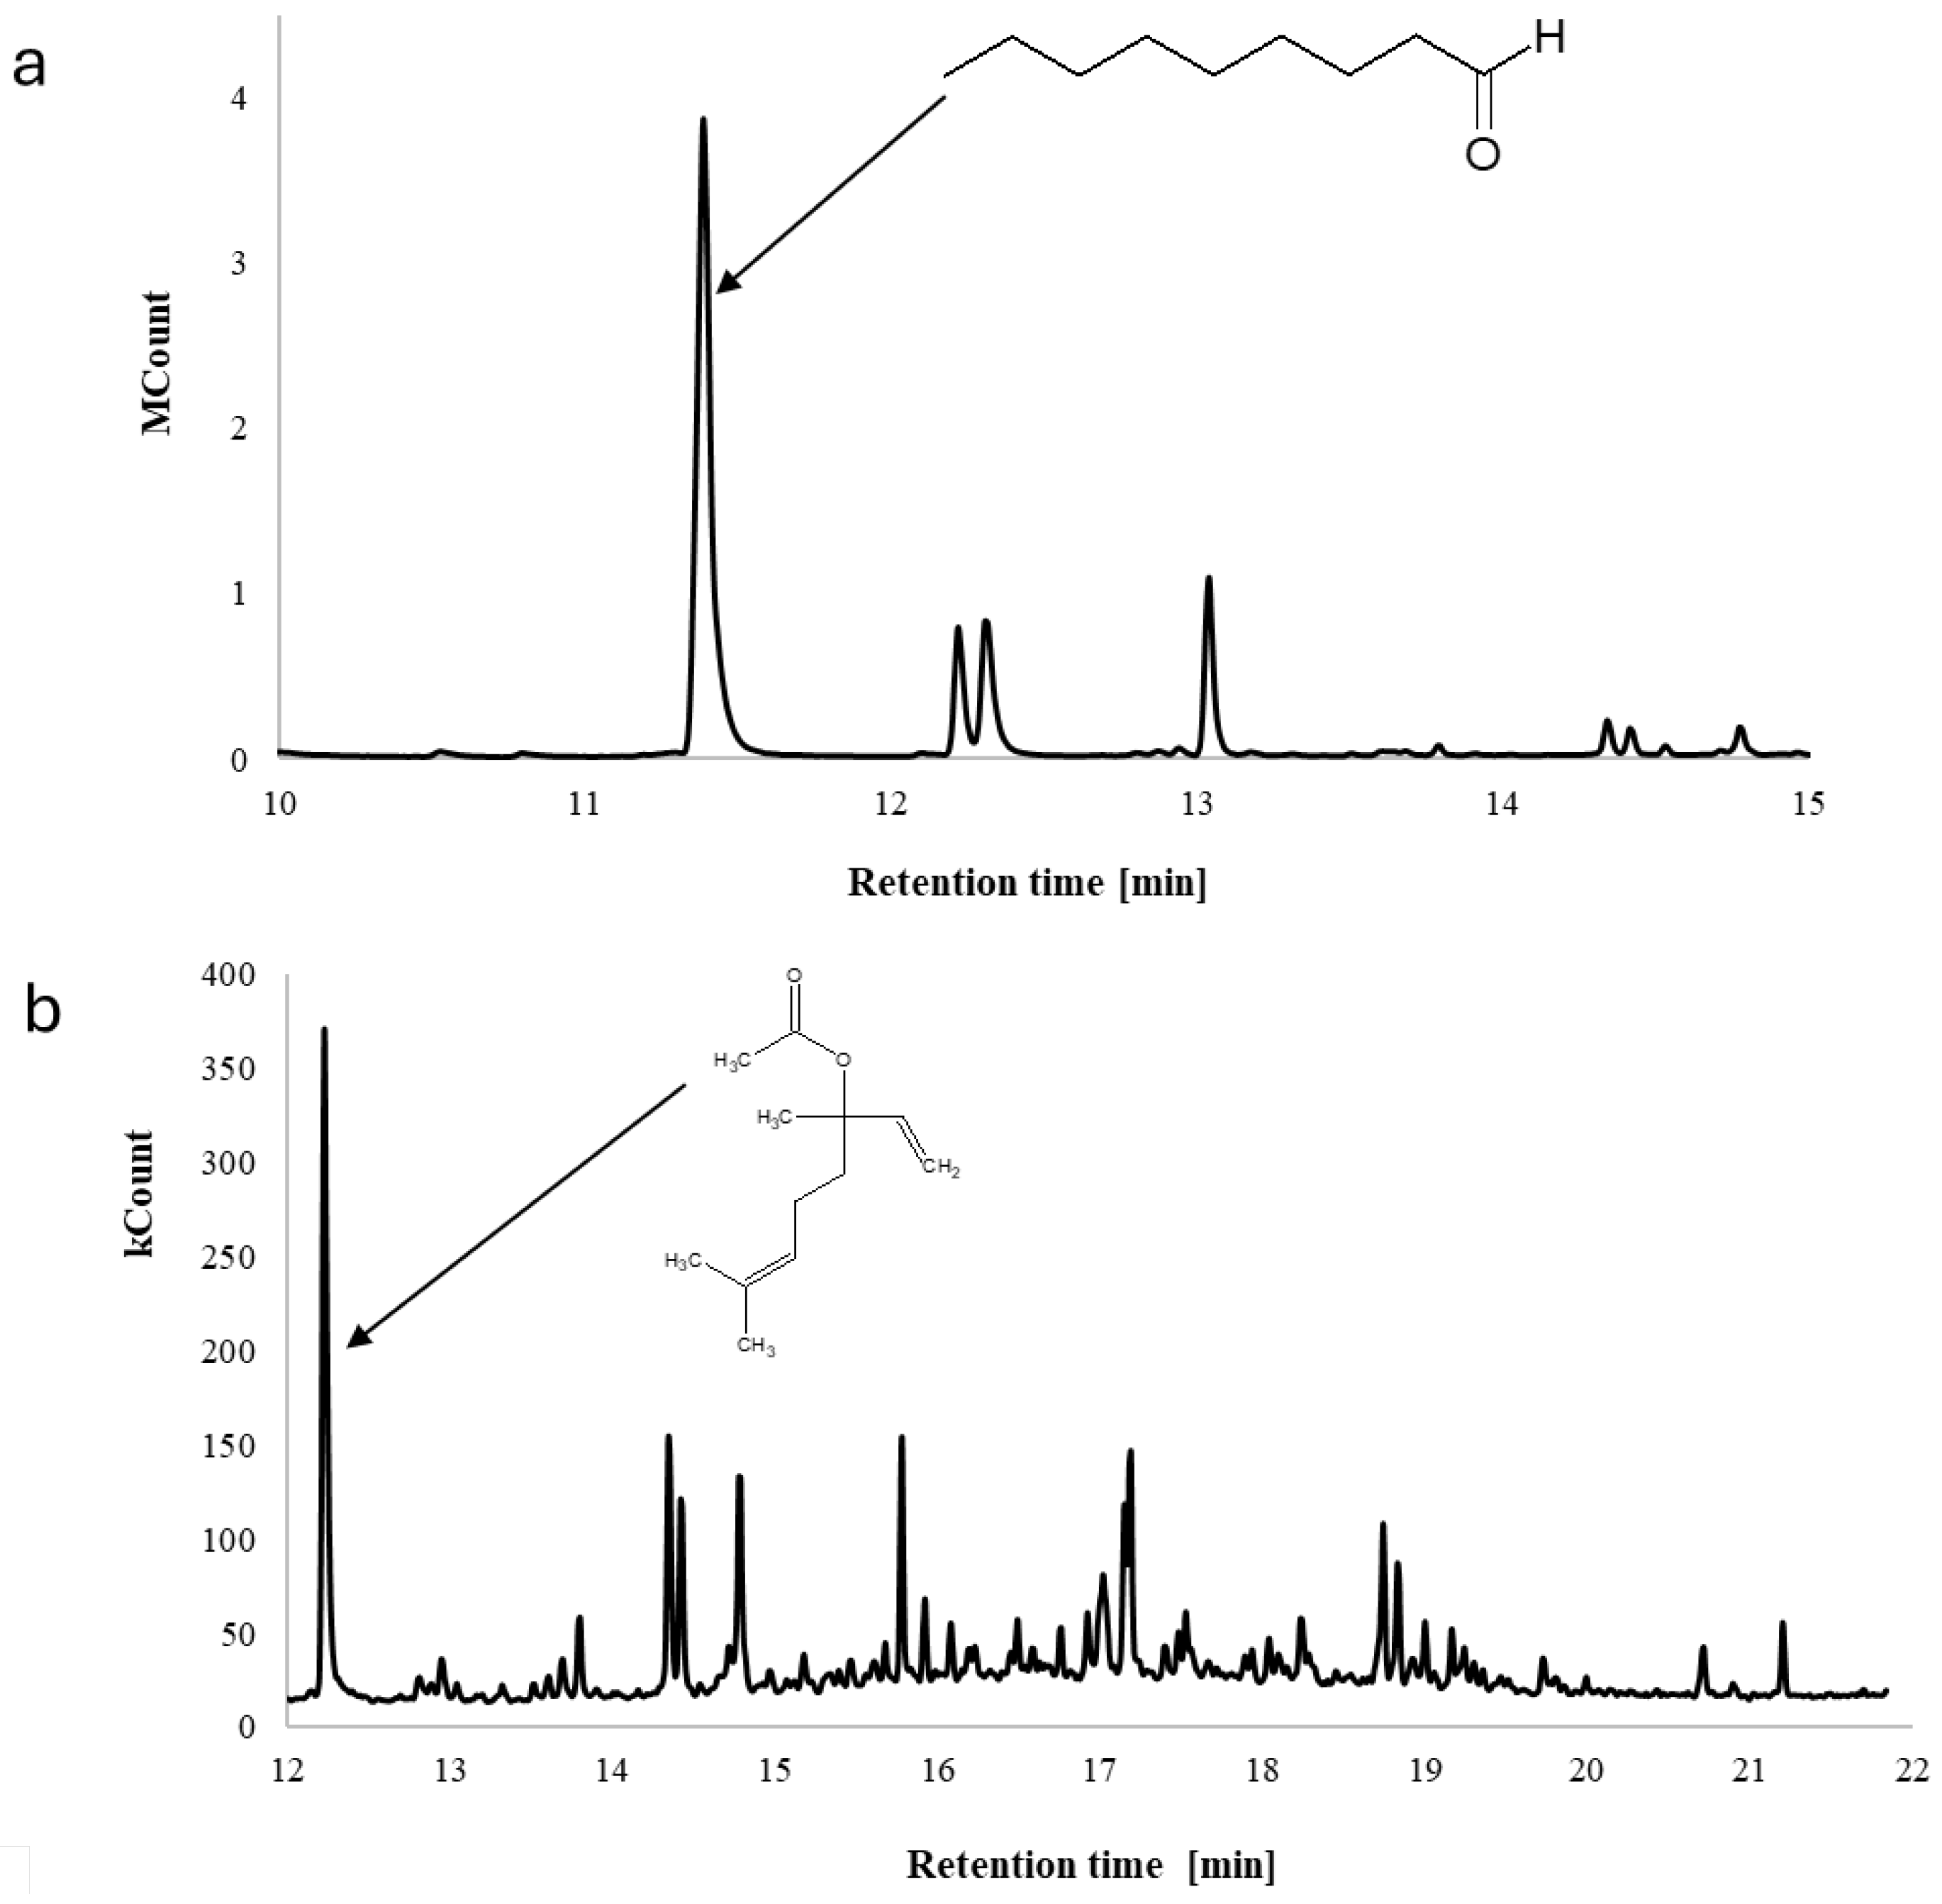
From the ozonated flour, six volatile compounds were isolated using the HS-SPME method (Table 2) The main group of volatile compounds was aldehydes (three), and one ester, one alcohol, and the heneicosane compound were identified. Non-analytical volatile compounds accounted for the highest percentage of all identified compounds (80.62%). The generation of the aldehydes was caused by the oxidation of the unsaturated fatty acids contained in the ozonated flour (Figure 1a), mainly omega 9 fatty acids. The control flour samples (non-ozonated) were also subjected to analysis. Within this sample, a group of three compounds were identified, two of which were also present in the ozonated sample (Figure 2 and Table 3).
Table 2.
Volatile compounds identified in ozonated flour.
Figure 1.
Chromatogram of volatile compounds isolated with the HS-SPME method from ozonated flour (a) and from control flour (b).
Figure 2.
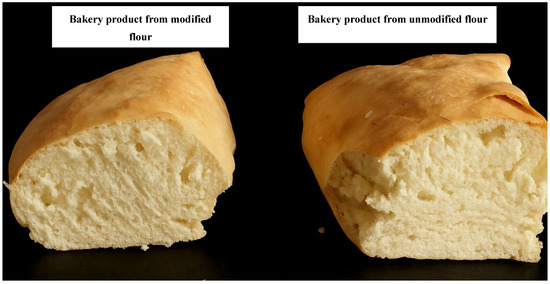
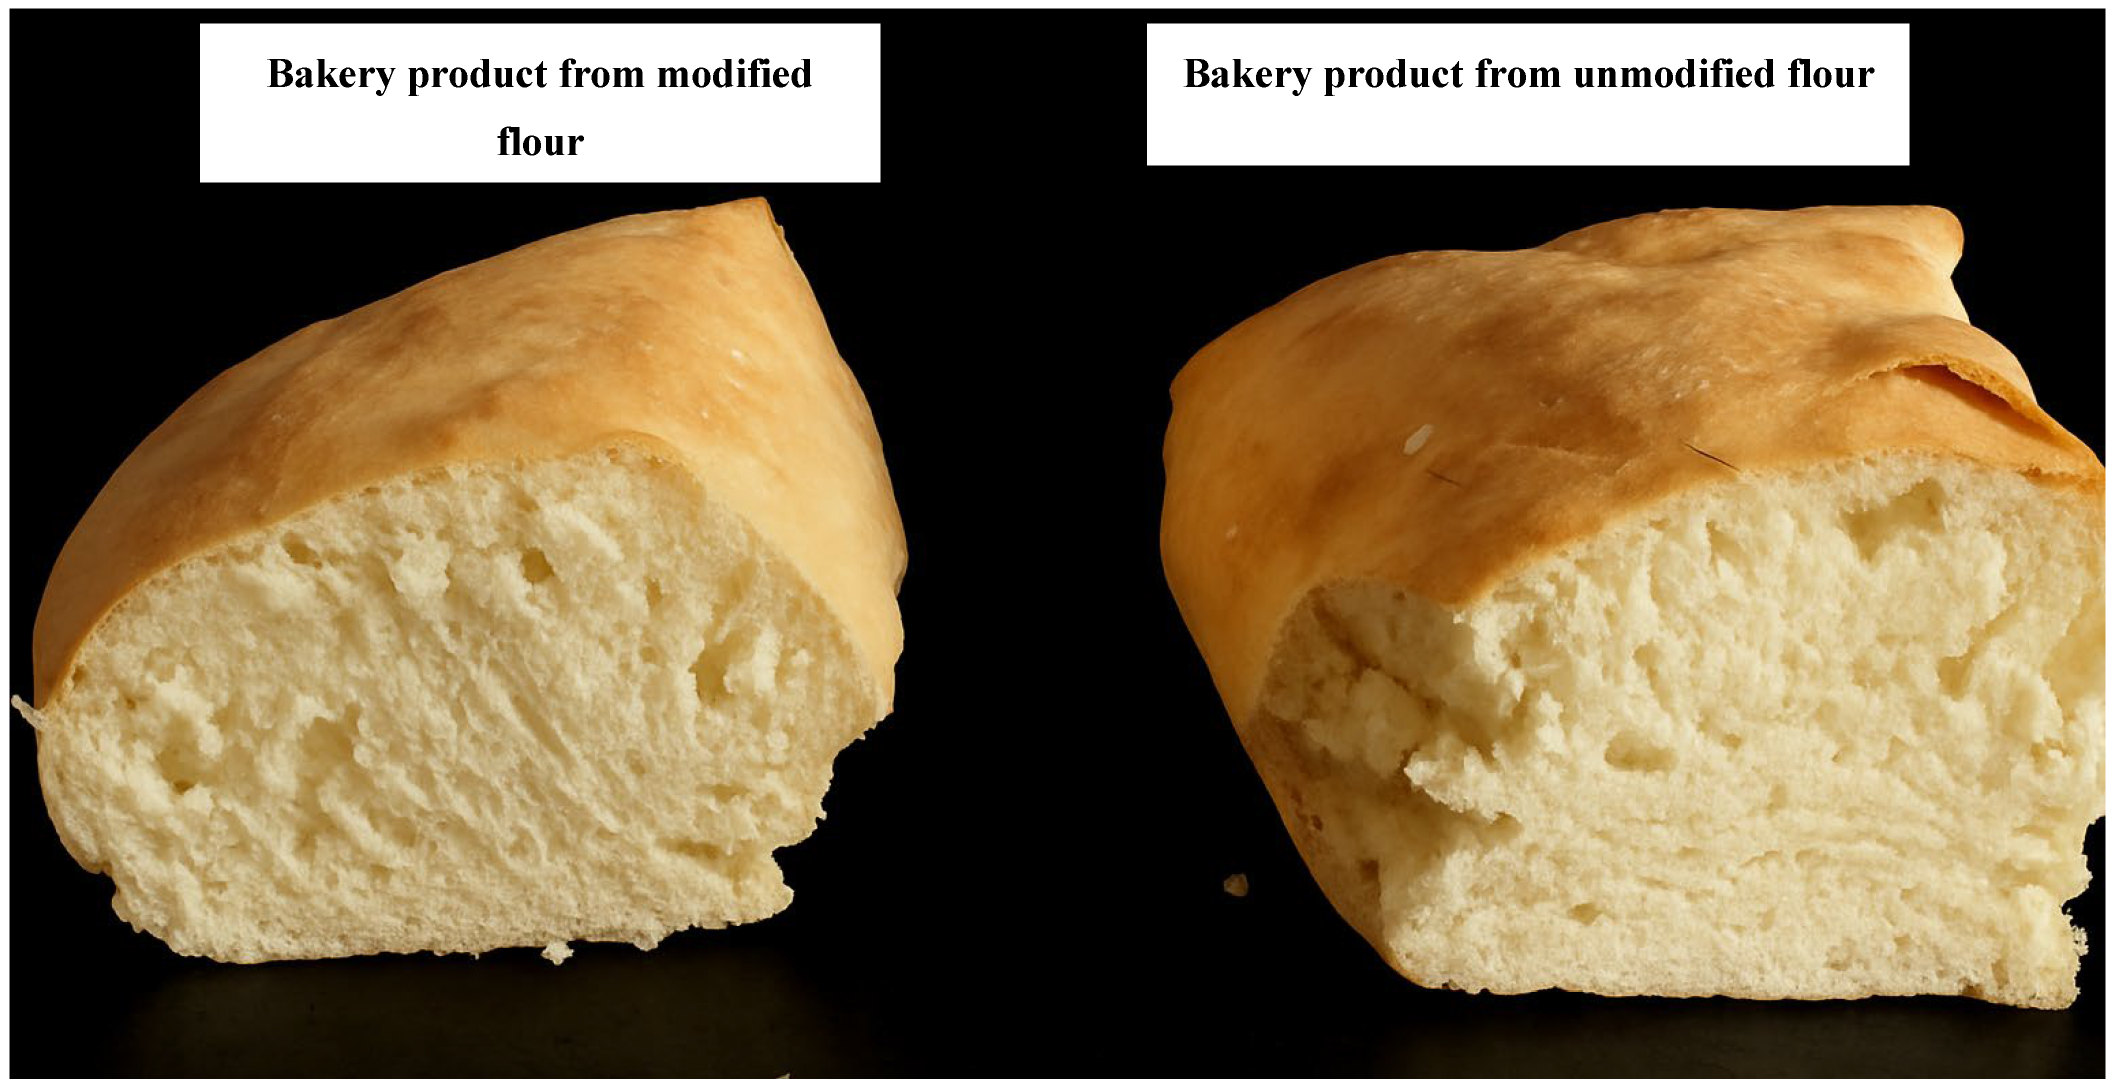
Comparison of bakery products prepared from modified and unmodified flour.
Table 3.
Volatile compounds identified in control flour (without ozonation).
The flour samples, including modified and control samples, were then utilised for the preparation of bakery products (Figure 2). These products were also subjected to analysis with the HS-SPME method (Table 4). Bakery products prepared from ozonated flour contained mostly nonanal, and some traces of tridecanal could be identified. It should be underlined that the intensity of these signals, defined as the peak area, was not higher than 3.3% of the signals observed in the case of flour analyses with HS-SPME method. This leads to a minimisation of the impact of these aldehydes on the final product. It should be noted that these aldehydes, including nonanal, are naturally present in food and are also produced under physiological conditions by humans [26]. Probably these compounds underwent thermal desorption during the preparation of bakery products. In particular, in the case of nonanal, which has a boiling temperature of 191 °C that is similar to the temperature of bakery product preparation, the desorption process could be initiated [27].
Table 4.
Volatile compounds identified in bakery products made from ozonated flour.
3.3. Evaluation of the Texture of Bakery Products
The texture profile analysis (TPA) was considered the most suitable test for objective comparation of the research samples prepared from the modified and control flours. The main texture parameters are summarised in Table 5. The results obtained were consistent with expectations; namely, bakery products prepared from ozonated flour obtained higher values in the gumminess, chewiness, and chewing index of hardness cycles 1 and 2 compared to bakery products made of unmodified flour, and also had the lowest elasticity index. The bakery products tested confirmed that ozonation significantly modified certain mechanical parameters, particularly hardness (cycles 1 and 2) and chewiness, which is presumably a consequence of changes in the activity of the flour’s enzymatic system. The flour ozonation process had an impact on the quality of the bakery products. The results obtained by Wang et al. [15] indicate that grain ozonation produced flour with higher strength and lower extensibility than native wheat flour. The authors of that study suggested that the generation of disulphide bonds is the main reaction responsible for the increase in the durability of the bakery products produced from ozonated grains and flour. The measurement of durability in both cycles e.g., 1 and 2, resulted in observation of higher values for the bakery products prepared from ozonated flour. The ozonation process also had a positive impact on the hardness of the bakery products prepared from ozonated wheat flour. Mei et al. [28] in their research observed that the ozonation procedure had a positive impact on the hardness of the prepared bakery product. In addition, elasticity and chewiness showed similar tendencies to hardness, which probably was a result of changes in the α-amylase and gluten content in the flour due to ozone treatment.
Table 5.
Results of the texture evaluation of the prepared bakery products.
The utilised ozone dose, amounting to 30 ppm for 30 min, was the maximal dose utilised by Piechowiak et al. [24]. In that work, the authors indicated that the dose of ozone has an impact on proteolytic, amylolytic, and lipolytic enzymes, which hypothetically, according to the authors, should modify to a greater degree the texturometric properties of cakes and bakery products made from them. The results presented confirm that the flour ozonation process significantly modifies the texture of baked goods. This is presumably caused by the fact that ozone oxidizes thiol groups in gluten proteins, potentially leading to the formation of disulphide bonds and a stronger, but less elastic, protein network, which manifests as increased hardness and chewiness [29].
3.4. Sensory Analysis of Bakery Products Prepared from Modified and Controlled Flour
The investigated bakery products were subjected to sensory evaluation using a five-point scale. The results of the evaluation are summarised in Table 6. Bakery products prepared with modified flour obtained a mean value of 3.04, while those prepared with control flour obtained a value of 3.74. This difference was caused by the worsening of the quality of the bakery products obtained from flour subjected to high concentrations of ozone, as reported in the literature [24].
Table 6.
Results of organoleptic evaluation with the five-point method (mean values were determined after multiplication by the importance indicator).
Under these conditions (high dose of ozone), a strong impact was observed on the final evaluation of bakery products. The results of the sensory analysis performed indicate good acceptability of the bakery products prepared from control flour and lower acceptability of the bakery products prepared from flour modified with ozone. The results obtained showed significant differences in taste and smell between the samples of the bakery products obtained. This is probably due to the specific smell of the decomposition products derived from the oxidation of fatty acids under the influence of ozone, which significantly influenced the evaluation of the smell and taste of the bakery products tested [30].
The colour of bakery products (Table 6) is an important feature that significantly affects the perception of the products by the consumer. In the research conducted, bakery products prepared from non-ozonated flour were characterised by a golden colour, an even colour of the crust, with a lighter or darker local colour. However, bakery products made of modified flour had an uneven, less golden colour on the entire surface. The colour of the crust of the analysed bakery products depended on the Maillard reaction occurring during baking, which results in the formation of compounds that give the food a brown colour, as well as the taste and aroma of the bakery products.
The change in crust colour was caused by the direct action of ozone gas on the flour components. Zhouliang et al. [31] showed in their research that ozonation made wheat flour whiter. Moreover, after analysing the results of the sensory evaluation of bakery products, it can be noticed that bakery products made of flour that was not subjected to the ozonation process were characterised by better flexibility, porosity, colour, and appearance of the crumb. The crumb of bakery products made of modified flour was insufficiently flexible; it exhibited clumping and large and small pores unevenly distributed in the crumb were visible, but the thickness of the crust was correct, although the side part of the crust had separated from the crumb. In addition, the structure of the unmodified flour dough was more sticky, and the dough was easier to knead compared to the modified flour dough, the texture of which was more “compact” and difficult to knead. The bakery products obtained from ozonated and non-ozonated flour differed from each other and showed different mechanical features (Table 6). Also, Zhouliang et al. [31] observed in their research that the activity of α-amylase was almost completely inhibited as a result of the direct use of ozone in the treatment of wheat flour. Wheat flour treated with ozone at a concentration of 60 mg L−1 for 2 h was significantly affected by ozone oxidation, resulting in a reduction in the wet gluten content, the gluten index, and the sedimentation volume. This resulted in a poorer quality of wheat flour, which was also characterised by poor stability of the flour gel, the lowest stability time, and increased development time of the cake. Piechowiak et al. [24] showed in their research that ozone in the gas phase significantly influences the activity of wheat flour enzymes, which are important in flour storage and processing.
4. Conclusions
The research conducted has shown that ozonation can significantly affect the selected quality parameters of flour, as well as cakes and bakery products made from it. The applied ozonation conditions caused changes in the composition of the volatile compounds that were isolated from the flour. These compounds were also identified in bakery products; however, it has been shown that they undergo the thermal desorption process to a large extent during the baking procedure. TPA analyses of the produced bakery products confirmed that ozonation significantly modifies some mechanical parameters, especially hardness (cycle 1 and 2) and chewiness, which is presumably a consequence of changes in the activity of the flour enzyme apparatus. The influence of the ozonation process was also demonstrated by organoleptic tests. Bakery products obtained from ozonated flour were found to be characterised by a poorer flavour–aroma profile compared to the control sample. However, it should be noted that extremely high doses of ozone gas described in the literature were used.
It should be noted that the microbiological analysis demonstrated that ozonation under the applied conditions contributed to a significant reduction in the overall microbiological load of the flour. A clear decrease in aerobic bacteria counts, as well as yeast and moulds, was observed in ozonated samples compared to the control, which confirms the high antimicrobial effectiveness of the treatment and its potential to improve the safety and shelf life of the raw material. In contrast, the number of lactic acid bacteria remained comparable in both variants, suggesting limited sensitivity of this group of microorganisms to the applied ozonation conditions or their naturally low initial presence in the analysed material. In general, these findings indicate that ozonation not only influences the physicochemical and sensory properties of flour and bakery products, but also effectively reduces their microbiological contamination, although the extent of these effects depends on the type of microorganisms and the parameters of the applied process.
Supplementary Materials
The following supporting information can be downloaded at: https://www.mdpi.com/article/10.3390/app16105115/s1, Table S1: Sensory Evaluation Sheet for Baked Products.
Author Contributions
Conceptualization, M.B.; methodology, M.B. and G.K.; validation, M.B.; formal analysis, P.A.; investigation, M.B., G.K., N.M., T.P. and J.M.; resources, J.M.; writing—original draft preparation, M.B. and N.M.; writing—review and editing, N.M.; visualisation, N.M. and M.B. All authors have read and agreed to the published version of the manuscript.
Funding
This research received no external funding.
Institutional Review Board Statement
Not applicable.
Informed Consent Statement
Not applicable.
Data Availability Statement
The data presented in this study are available in this article.
Conflicts of Interest
The authors declare no conflicts of interest.
References
- Bird, R.A.; Regina, A. High amylose wheat: A platform for delivering human health benefits. J. Cereal Sci. 2018, 82, 99–105. [Google Scholar] [CrossRef] [Scilit]
- Sheikholeslami, Z.; Mahfouzi, M.; Karimi, M.; Ghiafehdavoodi, M. Modification of dough characteristics and baking quality based on whole wheat flour by enzymes and emulsifiers supplementation. LWT 2021, 139, 110794. [Google Scholar] [CrossRef] [Scilit]
- Pandiselvam, R.; Subhashini, S.; Banuu Priya, E.P.; Kothakota, A.; Ramesh, S.V.; Shahir, S. Ozone based food preservation: A promising green technology for enhanced food safety. Ozone Sci. Eng. 2019, 41, 17–34. [Google Scholar] [CrossRef] [Scilit]
- Antos, P.; Szulc, J.; Ruman, T.; Balawejder, M.; Tereszkiewicz, K.; Kusz, B. Ozonation procedure for removal of mycotoxins in maize: A promising screening approach for improvement of food safety. PLoS ONE 2024, 19, e0310317. [Google Scholar] [CrossRef] [Scilit]
- Xue, W.; Macleod, J.; Blaxland, J. The Use of Ozone Technology to Control Microorganism Growth, Enhance Food Safety and Extend Shelf Life: A Promising Food Decontamination Technology. Foods 2023, 12, 814. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Mahmoud, Y.A.G.; Elkaliny, N.E.; Darwish, O.A.; Ashraf, Y.; Ebrahim, R.A.; Das, S.P.; Yahya, G. Comprehensive review for aflatoxin detoxification with special attention to cold plasma treatment. Mycotoxin Res. 2025, 41, 277–300. [Google Scholar] [CrossRef] [Scilit]
- Zhu, F. Effect of ozone treatment on the quality of grain products. Food Chem. 2018, 264, 358–366. [Google Scholar] [CrossRef] [Scilit]
- El Darra, N.; Xie, F.; Kamble, P.; Khan, Z.; Watson, I. Decontamination of Escherichia coli on dried onion flakes and black pepper using Infra-red, ultraviolet and ozone hurdle technologies. Heliyon 2021, 7, e07259. [Google Scholar] [CrossRef] [Scilit] [PubMed] [PubMed Central]
- Ouf, S.A.; Ali, E.M. Does the treatment of dried herbs with ozone as a fungal decontaminating agent affect the active constituents? Environ. Pollut. 2021, 277, 116715. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Sarron, E.; Gadonna-Widehem, P.; Aussenac, T. Ozone Treatments for Preserving Fresh Vegetables Quality: A Critical Review. Foods 2021, 10, 605. [Google Scholar] [CrossRef] [Scilit]
- Obadi, M.; Zhu, K.X.; Peng, W.; Sulieman, A.A.; Mohammed, K.; Zhou, H.M. Effects of ozone treatment on the physicochemical and functional properties of whole grain flour. J. Cereal Sci. 2018, 81, 127–132. [Google Scholar] [CrossRef] [Scilit]
- Paulikienė, S.; Žvirdauskienė, R. Evaluation of Hydrothermal Treatment of Winter Wheat Grain with Ozonated Water. Plants 2023, 12, 3267. [Google Scholar] [CrossRef] [Scilit]
- Enríquez-Castro, C.M.; Pérez-Nafarrate, M.; Gerardo Rodríguez, J.E. Innovation in Food Products Using Ozone Technology: Impact on Quality Assurance. In Innovation in the Food Sector Through the Valorization of Food and Agro-Food By-Products; IntechOpen: London, UK, 2020. [Google Scholar] [CrossRef] [Scilit]
- Granella, S.J.; Bechlin, T.R.; Christ, D.; Machado, C.S.R. Kinetic and physicochemical properties of drying-ozonation process on wheat grain. J. Food Process. Preserv. 2019, 43, e14057. [Google Scholar] [CrossRef] [Scilit]
- Wang, L.; Shao, H.; Luo, X.; Wang, R.; Li, Y.; Li, Y.; Luo, Y.; Chen, Z. Effect of Ozone Treatment on Deoxynivalenol and Wheat Quality. PLoS ONE 2016, 11, e0147613. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Zhang, W.; Li, L.; Shu, Z.; Wang, P.; Zeng, X.; Shen, W.; Ding, W.; Shi, Y.C. Properties of flour from pearled wheat kernels as affected by ozone treatment. Food Chem. 2021, 341, 128203. [Google Scholar] [CrossRef] [Scilit]
- Alexandre, A.P.S.; Castanha, N.; Costa, N.S.; Santos, A.S.; Badiale-Furlong, E.; Augusto, P.E.D.; Calori-Domingues, M.A. Ozone technology to reduce zearalenone contamination in whole maize flour: Degradation kinetics and impact on quality. J. Sci. Food Agric. 2019, 99, 6814–6821. [Google Scholar] [CrossRef] [Scilit]
- Shahidi, F.; Hossain, A. Role of Lipids in Food Flavor Generation. Molecules 2022, 27, 5014. [Google Scholar] [CrossRef] [Scilit]
- Matłok, N.; Piechowiak, T.; Zardzewiały, M.; Gorzelany, J.; Balawejder, M. Effects of Ozone Treatment on Microbial Status and the Contents of Selected Bioactive Compounds in Origanum majorana L. Plants. Plants 2020, 9, 1637. [Google Scholar] [CrossRef] [Scilit]
- Wójcik, M.; Dziki, D.; Matwijczuk, A.; Gawlik-Dziki, U. Walnut Flour as an Ingredient for Producing Low-Carbohydrate Bread: Physicochemical, Sensory, and Spectroscopic Characteristics. Foods 2023, 12, 3320. [Google Scholar] [CrossRef] [Scilit]
- Hamid, Z.; Meyrick, B.K.; Macleod, J.; Heath, E.A.; Blaxland, J. The application of ozone within the food industry, mode of action, current and future applications, and regulatory compliance. Lett. Appl. Microbiol. 2024, 77, ovae101. [Google Scholar] [CrossRef] [Scilit]
- Wang, L.; Luo, Y.; Luo, X.; Wang, R.; Li, Y.; Li, Y.; Shao, H.; Chen, Z. Effect of deoxynivalenol detoxification by ozone treatment in wheat grains. Food Control 2016, 66, 137–144. [Google Scholar] [CrossRef] [Scilit]
- Feng, T.; Wang, J. Oxidative stress tolerance and antioxidant capacity of lactic acid bacteria as probiotic: A systematic review. Gut Microbes 2020, 12, 1801944. [Google Scholar] [CrossRef] [Scilit]
- Piechowiak, T.; Józefczyk, R.; Balawejder, M. Impact of ozonation process of wheat flour on the activity of selected enzymes. J. Cereal Sci. 2018, 84, 30–37. [Google Scholar] [CrossRef] [Scilit]
- Zhou, Z.; Lakey, P.S.J.; von Domaros, M.; Wise, N.; Tobias, D.J.; Shiraiwa, M.; Abbatt, J.P.D. Multiphase Ozonolysis of Oleic Acid-Based Lipids: Quantitation of Major Products and Kinetic Multilayer Modeling. Environ. Sci. Technol. 2022, 56, 7716–7728. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Pathak, A.; Swargiary, K.; Kongsawang, N.; Jitpratak, P.; Ajchareeyasoontorn, N.; Udomkittivorakul, J.; Viphavakit, C. Recent Advances in Sensing Materials Targeting Clinical Volatile Organic Compound (VOC) Biomarkers: A Review. Biosensors 2023, 13, 114. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Pico, J.; Gómez, M.; Bernal, J.; Bernal, J.L. Analytical methods for volatile compounds in wheat bread. J. Chromatogr. A 2016, 1428, 55–71. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Mei, J.; Liu, G.; Huang, X.; Ding, W. Effects of ozone treatment on medium hard wheat (Triticum aestivum L.) flour quality and performance in steamed bread making. CyTA-J. Food 2016, 14, 449–456. [Google Scholar]
- Abedi, E.; Pourmohammadi, K. The effect of redox agents on conformation and structure characterization of gluten protein: An extensive review. Food Sci. Nutr. 2020, 8, 6301–6319. [Google Scholar] [CrossRef] [Scilit]
- Premjit, Y.; Sruthi, N.U.; Pandiselvam, R.; Kothakota, A. Aqueous ozone: Chemistry, physiochemical properties, microbial inactivation, factors influencing antimicrobial effectiveness, and application in food. Compr. Rev. Food Sci. Food Saf. 2022, 21, 1054–1085. [Google Scholar] [CrossRef] [Scilit]
- Zhuang, K.; Sun, Z.; Huang, Y.; Lyu, Q.; Zhang, W.; Chen, X.; Wang, G.; Ding, W.; Wang, Y. Influence of different pretreatments on the quality of wheat bran-germ powder, reconstituted whole wheat flour and Chinese steamed bread. LWT 2022, 161, 113357. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.