


Abstract
In the present study, the effects of electrode geometry and welding current on the tensile-shear strength, failure energy, fracture type, and joint microstructure were investigated during the RSW of ultra-high-strength MS1500 steel to high-strength low-alloy SPFC590 steel, both 1.2 mm in thickness. Three electrode geometries—designated as G0-6 mm, G0-8 mm, and A0—recommended for 1.2 mm sheets according to ISO 5821 were examined. It was found that in the G0-6 mm electrode geometry, which has the smallest contact area, excessive expulsion occurred at lower current levels compared to the other geometries. Consequently, this configuration resulted in lower maximum tensile-shear strength and failure energy values. The highest mechanical performance was achieved with the G0-8 mm electrode geometry, where the tensile-shear strength and failure energy were measured as 19.42 kN and 43.81 J, respectively. For the A0 electrode, although the maximum tensile-shear strength (19.68 kN) was comparable to that of the G0-8 mm geometry, the failure energy was approximately 7% lower (40.94 J). For all electrode geometries corresponding to maximum mechanical strength, a pull-out failure mode was observed, where the nugget region of the SPFC590 steel detached from the base metal and remained adhered to the ultra-high-strength MS1500 sheet.
1. Introduction
Resistance spot welding (RSW) is widely utilized in the automotive industry due to its high efficiency, flexibility, and compatibility with automation. These advantages make it a preferred method for joining advanced high-strength steels (AHSS), enabling lightweight designs without compromising structural integrity [1]. A typical passenger vehicle may contain several thousand RSW joints, particularly in critical safety-related components. Consequently, the mechanical integrity of these welds plays a crucial role in determining the crashworthiness of vehicle structures [2]. Therefore, improving the mechanical strength and reliability of RSW joints is of paramount importance.
The mechanical strength of a resistance spot weld is influenced by several factors, among which the nugget diameter plays a decisive role. It is well established that a larger nugget diameter generally leads to higher joint strength [3,4,5]. This is attributed to the increase in the load-bearing cross-sectional area as the nugget size grows. Consequently, the joint can sustain higher forces before failure. With increasing nugget diameter, the dominant failure mode typically shifts from interfacial fracture (along the faying surface) to pull-out fracture (through the thickness of the nugget) [6,7].
In order to increase the nugget diameter without expulsion formation, it is necessary to determine the optimum value of the welding current and duration. Expulsion is defined as ejection out of the molten metal out of the welding zone caused by the pressure in the liquid metal that melts and expands in the nugget zone, if it cannot be balanced by the force applied over welding electrodes. When expulsion occurs, even though the nugget diameter may increase, the mechanical strength of the joint typically decreases [8]. Therefore, in order to achieve the highest possible joint strength, welding parameters—particularly the welding current—must be carefully adjusted to prevent expulsion and to ensure pull-out fracture behavior.
Numerous studies have examined the influence of welding current on the mechanical properties of RSW joints, including applications involving AHSS materials [9,10,11,12,13,14,15,16,17,18,19]. These studies have highlighted that the mechanical strength is governed not only by the nugget diameter but also by the microstructure of the nugget and the heat-affected zone (HAZ). Thus, a comprehensive understanding of both geometrical and microstructural characteristics, as well as the corresponding failure modes, is crucial for predicting the performance of RSW joints.
In recent years, the increasing demand for lightweight structures has driven the use of dissimilar material combinations to exploit the unique properties of each component. RSW has proven to be an effective technique for joining such materials. Several studies have demonstrated the applicability of RSW to join advanced high-strength steel sheets of different grades and thicknesses depending on specific design requirements [20,21,22,23,24,25,26,27]. Most of these investigations, however, focus on dual-phase steels, where the mechanical strengths of the joined sheets do not differ significantly. Nevertheless, current industrial applications often require the joining of steels with markedly different mechanical properties. Such material pairings are frequently used, particularly in the bumper beam regions of passenger vehicles.
In the present study, the RSW characteristics of ultra-high-strength MS1500 steel and cold-rolled high-strength low-alloy SPFC590 steel were investigated. The main focus was on evaluating the effects of welding current and electrode geometry on the mechanical strength, joint geometry, fracture behavior, and microstructure of 1.2 mm thick steel sheets.
2. Materials and Methods
Materials used in this study were martensitic micro-structured ultra-high-strength MS1500 steel and cold rolled high-strength low alloy SPFC590 steel both with a thickness of 1.2 mm. The material’s mechanical properties were evaluated using specimens with a nominal width of 12.5 mm and a gauge length of 50 mm, following the ISO 6892-1:2019 standard [28]. A total of five tests were performed, and the average results are summarized in Table 1.
Table 1.
Mechanical properties of the investigated materials.
The chemical compositions of the steels used in this study are listed in Table 2. MS1500 steel contains 0.271 wt.% carbon and 0.770 wt.% manganese, whereas SPFC590 steel exhibits a significantly lower carbon content but a relatively higher manganese content of approximately 1.540 wt.%. Consequently, both steels are expected to undergo martensitic transformation in their microstructures upon rapid cooling from the austenitic region.
Table 2.
Measured alloy composition of the investigated materials (weight %).
When Table 1 and Table 2 are examined together, it is evident that the investigated steel pair exhibits significant differences in both mechanical properties and chemical composition. From the mechanical point of view, there is a difference of 865 MPa in yield strength and 895 MPa in ultimate tensile strength between the two materials. In addition, the elongation at fracture of SPFC590 steel, with a value of 34.1%, is considerably higher than that of the MS1500 steel. A similar contrast is observed in the chemical compositions. While the carbon content of MS1500 steel is relatively high at 0.271%, SPFC590 steel contains only 0.071% carbon. Conversely, the manganese content of SPFC590 steel is significantly higher, with a value of 1.540%, compared to 0.770% for MS1500 steel. These differences are expected to strongly affect the nugget formation and fracture behavior during the RSW process. Furthermore, the carbon equivalent values of the investigated materials were calculated according to Equation (1). Based on this equation, the carbon equivalent values of the MS1500 and SPFC590 steels were determined to be 41.0% and 32.7%, respectively.
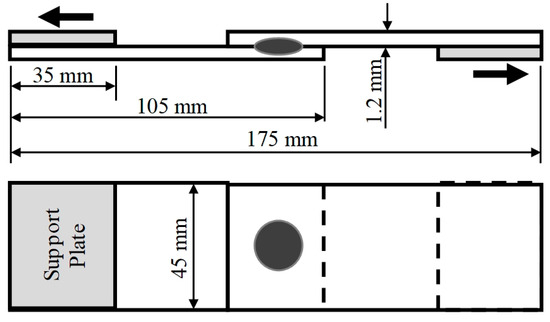
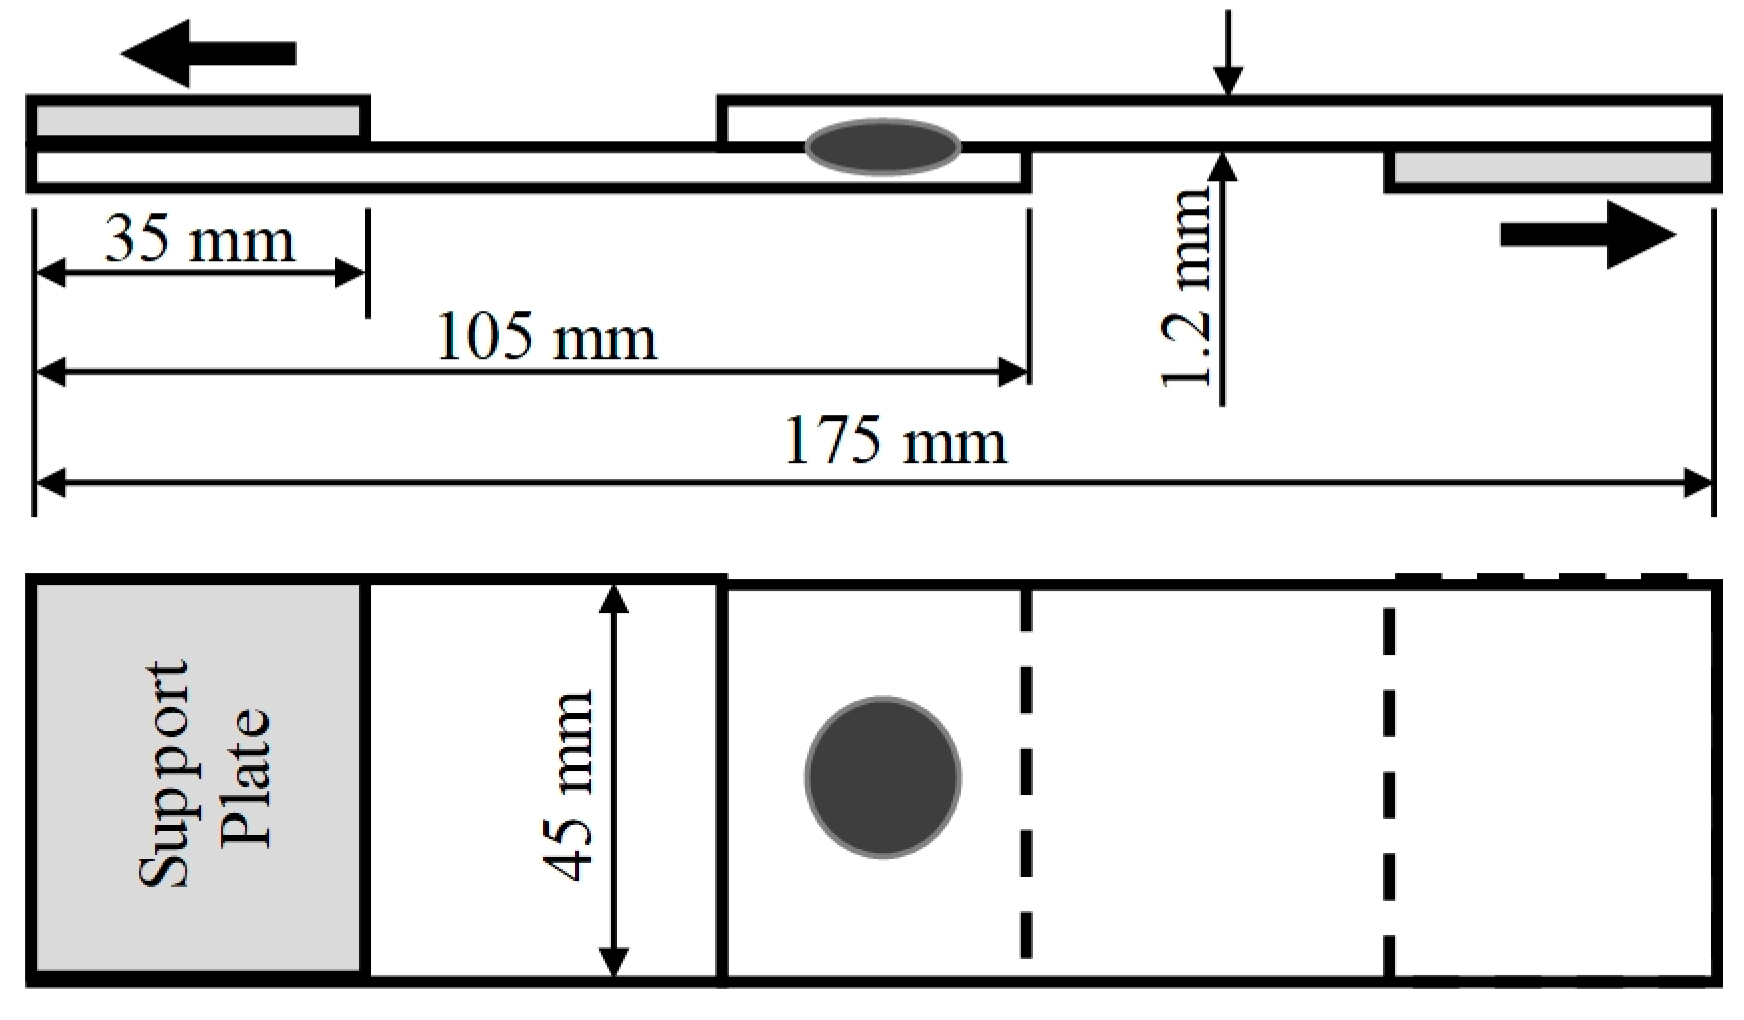
The specimens used for the RSW experiments were mechanically cut to dimensions of 105 × 45 mm in accordance with the ISO 14273:2016 standard [29]. The samples were positioned and welded as illustrated in Figure 1, following the requirements of the same standard. During welding, the SPFC590 sheets were consistently placed on the upper side, whereas the MS1500 sheets were positioned on the lower side. Prior to welding, the faying surfaces of all specimens were cleaned with acetone to remove any contaminants that could affect the electrical resistance and weld quality. After welding, additional support plates were attached to minimize deformation in the nugget area during the subsequent tensile-shear tests. The arrows shown in Figure 1 indicate the loading direction applied during these tests.
Figure 1.
Schematic view of resistance spot-welded tensile-shear test specimens (all dimensions in mm).
All welding experiments were conducted using a water-cooled, pneumatically operated, pedestal-type RSW machine with a rated capacity of 70 kVA. The machine was equipped with numerical control for regulating the welding current, weld time, and electrode force with high precision. It operates at a frequency of 50 Hz.
The main welding parameters in this study were selected based on the recommendations of the American Welding Society (AWS) [30]. For all welding operations, the electrode force was maintained at 3.4 kN. The welding duration was fixed at 12 cycles, corresponding to 0.24 s, while the hold time after welding was set to 20 cycles (0.40 s) [31]. The squeeze time prior to welding and the electrode release time after each welding operation were both adjusted to 50 cycles to ensure consistent contact pressure and controlled cooling conditions.
To investigate the influence of welding current on joint formation, geometrical properties, and mechanical behavior, the welding current was varied from 7 kA to 13 kA in 0.5 kA increments. The lower limit of 7 kA was selected as the minimum current required to ensure stable nugget formation without interfacial failure, while the upper limit of 13 kA was determined to avoid excessive expulsion, severe electrode wear, and surface indentation. This current range also covers the typical operating window used in industrial resistance spot welding of ultra-high strength steels with similar thicknesses.
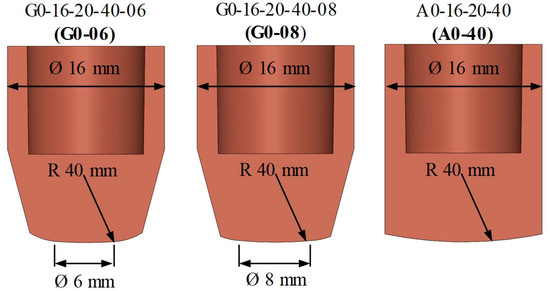
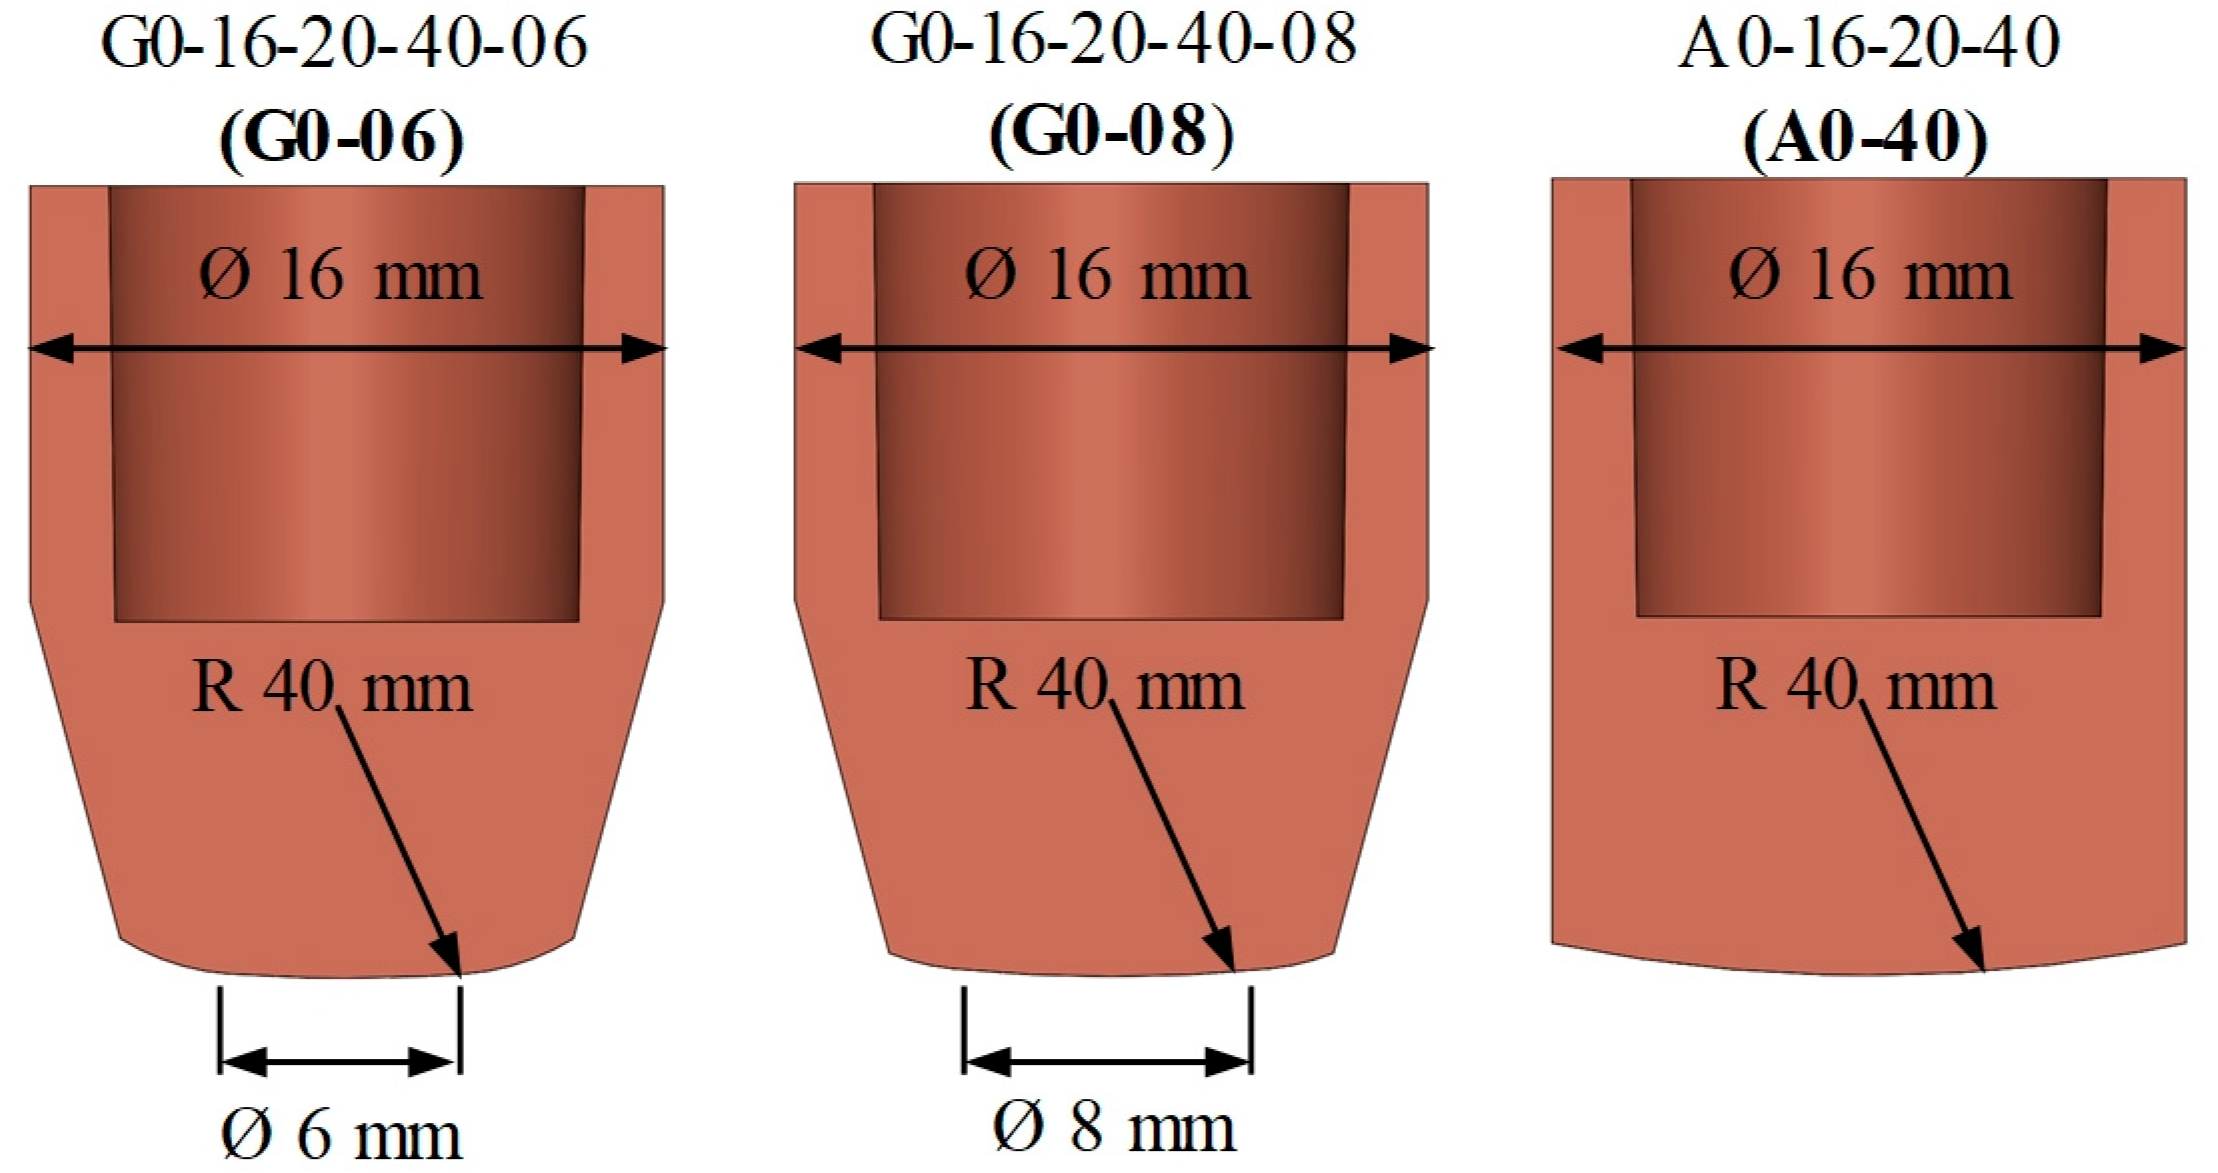
In this study, the effects of three different electrode tip geometries on the mechanical strength, weld geometry, and failure mode of the RSW joints were investigated. The electrodes were selected in accordance with the ISO 5821:2025 standard and designated as G0-16-20-40-06, G0-16-20-40-08, and A0-16-20-40 [32]. All electrodes were manufactured from type A 2/3 copper alloyed with chromium and zirconium, as specified by ISO 5182:2016 [33]. For simplicity, these geometries are hereafter referred to as G0-06, G0-08, and A0-40, respectively. The schematic representations of the electrode tip geometries are illustrated in Figure 2. Each electrode type differs primarily in its tip radius and included angle, which directly influence the current density distribution and heat generation at the faying interface, thereby affecting nugget formation and mechanical performance of the welded joints.
Figure 2.
Schematic view of used electrode geometries.
After welding, the joints were subjected to tensile-shear testing to evaluate their load-bearing capacity and fracture behavior. For each welding current level investigated in this study, ten welded specimens were prepared. To ensure the statistical reliability of the tensile-shear test results, nine of these specimens were used for testing. All tests were carried out in accordance with the ISO 14273:2016 standard using a servo-mechanical UTEST UTM-500 universal tensile testing machine (UTEST, Ankara, Türkiye) with a maximum load capacity of 50 kN and a constant crosshead speed of 10 mm/min.
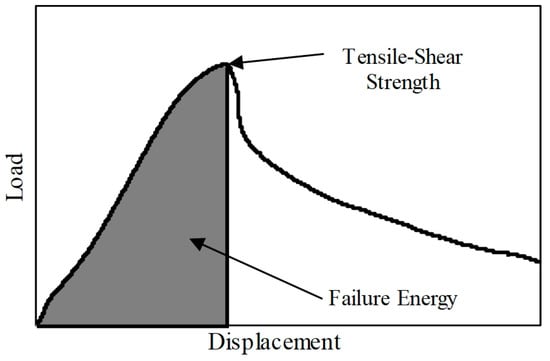
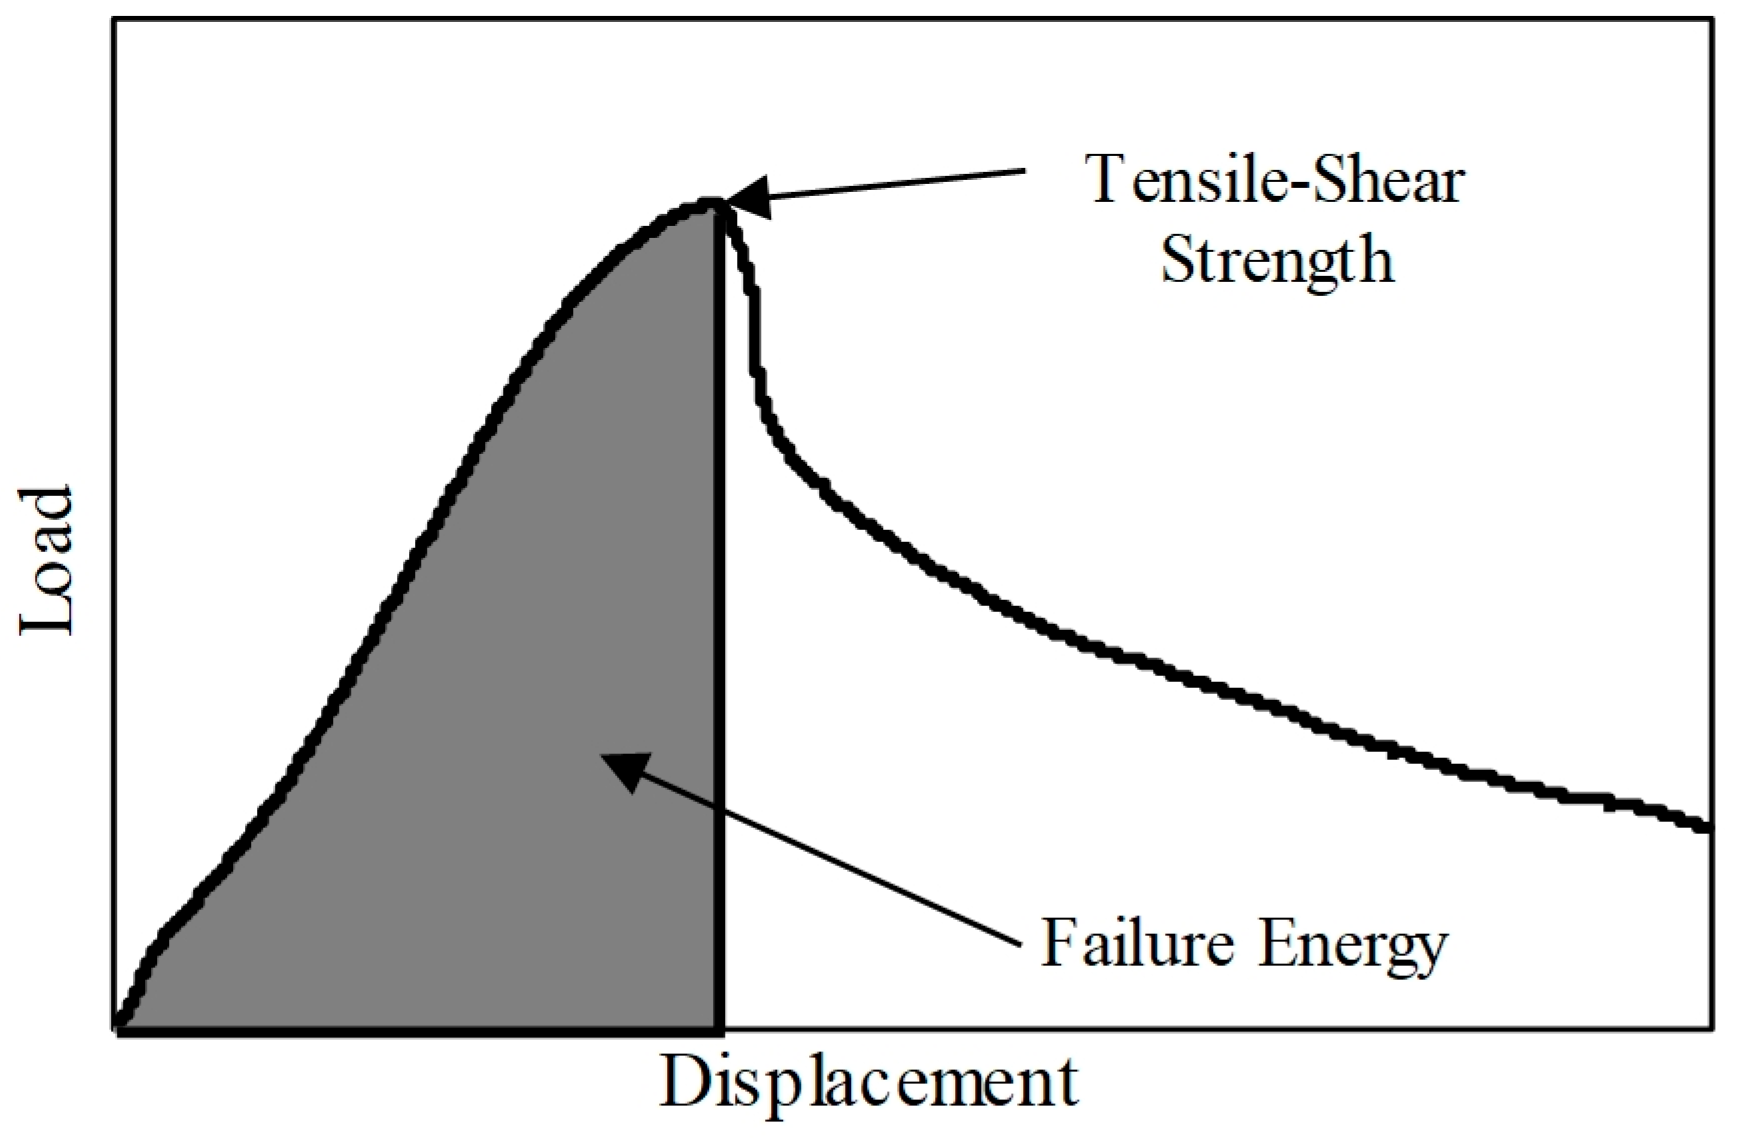
The tensile-shear strength and fracture energy of the joints were derived from the corresponding force–displacement curves, as illustrated in Figure 3. The peak value on each curve represents the tensile-shear strength of the joint, while the fracture energy (FE) was calculated as the area under the curve up to the maximum load point, according to the following Equation (2):
where F is the applied load (N), x is the displacement (mm), n is the total number of data points, and nmax denotes the data point corresponding to the maximum measured force.
Figure 3.
Schematic representation of load–displacement curve results of tensile-shear tests.
After mechanical testing, selected samples were sectioned for metallographic and microstructural analyses to better understand the influence of welding parameters and electrode geometry on joint formation. One of the welded specimens was specifically prepared for geometric and microstructural examination. For this purpose, the specimen was abrasively sectioned through the center of the weld and mounted in cold-setting bakelite. The cross-sections were then ground using silicon carbide papers with grit sizes ranging from P400 to P2500 and subsequently polished with a 1 µm diamond suspension.
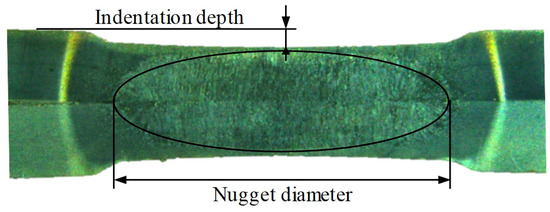
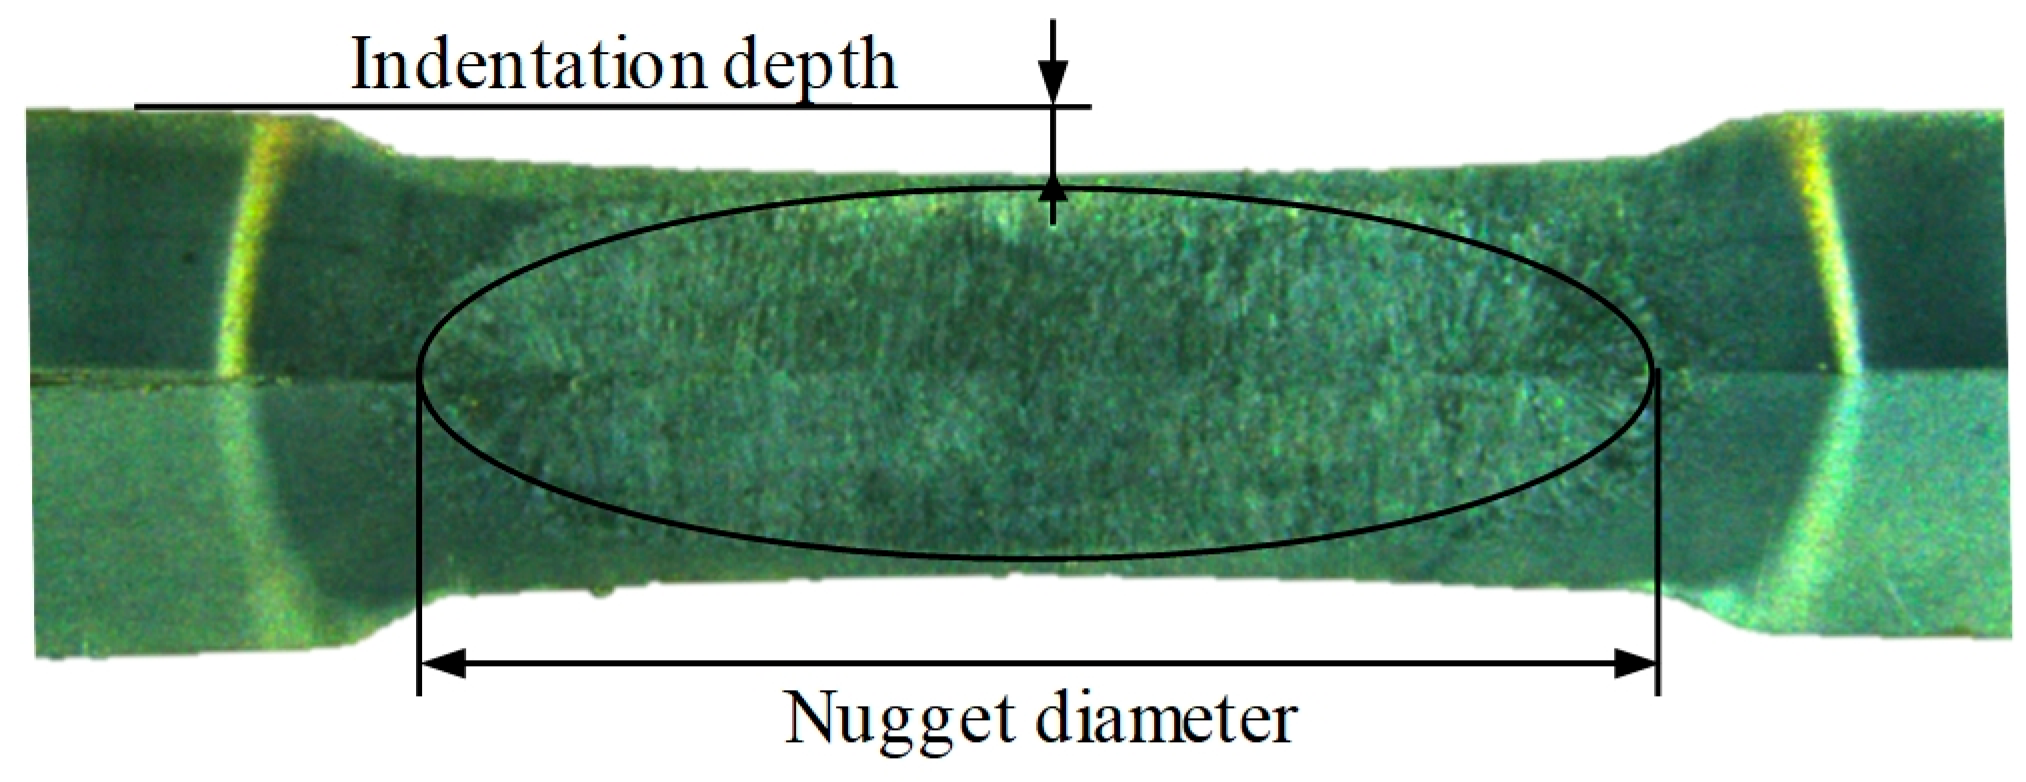
To reveal the microstructure and enable geometric measurements, the polished specimens were etched with a 4% Nital solution for approximately 10 s. Optical observations and measurements were performed using an Optika IM-3MET optical microscope (Optika, Ponteranica, Italy). In this study, particular attention was given to the determination of nugget diameter and electrode indentation geometry. Representative examples of the measured geometrical features are presented in Figure 4.
Figure 4.
Example of geometric parameter measurements on weld cross-section.
Additionally, microhardness mapping was carried out across the weld cross-sections to evaluate the mechanical property gradients between the base metal, heat-affected zone (HAZ), and nugget regions. The hardness measurements were performed in accordance with the ISO 6507-1:2018 standard using a Future Tech FM-700e microhardness tester (Future-Tech, Kawasaki-City, Japan) under a load of 100 g and a dwell time of 15 s [34]. Indentations were placed along a measurement line extending from the base metal of the SPFC590 sheet, passing through the weld nugget, and continuing into the base metal of the MS1500 steel.
Further microstructural characterization was performed using scanning electron microscopy (SEM) to identify the phase transformations and microstructural features formed during the resistance spot welding process. Microstructure analyses were carried out using a Hitachi SU5000 scanning electron microscope (Hitachi, Ibaraki, Japan). The observations focused on the nugget, heat-affected zone (HAZ), and base metal regions to investigate the morphological differences resulting from variations in welding current and electrode geometry.
3. Results and Discussion
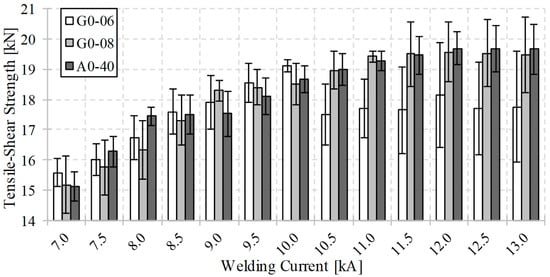
The tensile-shear strength results obtained from the resistance spot-welded joints are summarized in Figure 5. Each data point represents the average value of nine individual measurements, and the corresponding error bars indicate the standard deviations calculated from these measurements. At a welding current of 7.0 kA, all electrode geometries exhibited nearly identical tensile-shear strength values. For the G0-06 electrode geometry, the highest strength was recorded at a welding current of 10.0 kA, after which both a noticeable decrease in strength and an increase in standard deviation were observed. In the case of the G0-08 geometry, the tensile-shear strength increased up to 11.0 kA, beyond which no further improvement occurred, accompanied by a rise in standard deviation values. For the A0-40 geometry, the increase in tensile-shear strength slowed markedly after 11.0 kA, reaching its maximum at 12.0 kA. At higher current levels, the strength values remained almost constant, while the standard deviations continued to increase. The highest average tensile-shear strength was measured for the A0-40 geometry at 19.68 kN, followed by 19.28 kN for G0-08 and 18.51 kN for G0-06.
Figure 5.
Tensile-shear strength results depending on the electrode geometry and welding current.
According to the AWS C1.1M/C1.1:2019 standard, the minimum acceptable tensile-shear strength of a spot weld can be estimated based on the sheet thickness and the tensile strength of the weaker material [30]. Minimum acceptable tensile-shear strength of SPFC590 material with a thickness of 1.2 mm is calculated as 11.9 kN. All welds produced under the investigated parameter ranges exhibited higher tensile-shear strength values than the minimum requirements.
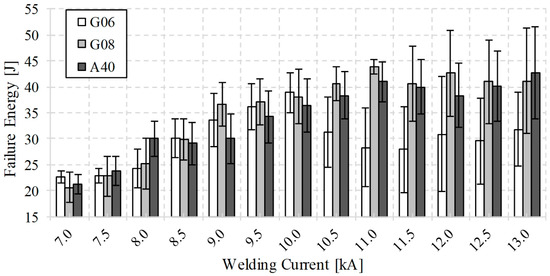
The variation in failure energy with welding current for the different electrode geometries is presented in Figure 6. As in the tensile-shear strength results, each value corresponds to the average of nine individual measurements, and the error bars indicate the associated standard deviations. At a welding current of 7.0 kA, all electrode geometries exhibited nearly identical failure energy values. For the G0-06 electrode geometry, the failure energy increased steadily up to a welding current of 10.0 kA, followed by a pronounced decrease at higher current levels. A similar trend was observed for the G0-08 geometry, where the failure energy rose up to 11.0 kA and then dropped noticeably, accompanied by an increase in standard deviation values. In the case of the A0-40 geometry, the highest failure energy was measured at a welding current of 11.0 kA, unlike the tensile-shear strength results. Further increase in current led to a decline in energy values and a rise in standard deviation. The maximum failure energy values were recorded as 38.13 J, 43.81 J, and 40.94 J for the G0-06, G0-08, and A0-40 electrode geometries, respectively. When the obtained tensile–shear strength values are compared with those reported in the literature, it can be seen that the mechanical strength achieved for the dissimilar joints lies between the values obtained when the individual base materials are welded to themselves. For SPFC590 steel, tensile–shear strength values of up to 18 kN have been reported after resistance spot welding with similar materials [10,21,22,35]. In contrast, when martensitic steels are joined by resistance spot welding, tensile–shear strength values exceeding 25 kN can be achieved [15]. However, in the case of welding two dissimilar materials, the newly formed material in the nugget region—resulting from the mixing of the molten base materials—exhibits mechanical strength values that fall between those of the two base materials. This behavior has also been reported for other welded joints involving dissimilar materials [17,20,21].
Figure 6.
Failure energy results depending on the electrode geometry and welding current.
To interpret the tensile-shear strength and failure energy results more comprehensively, it is necessary to evaluate them together with the tensile-shear load versus displacement curves obtained at different welding currents, as well as the corresponding nugget diameter, failure type, expulsion formation, and electrode indentation values.
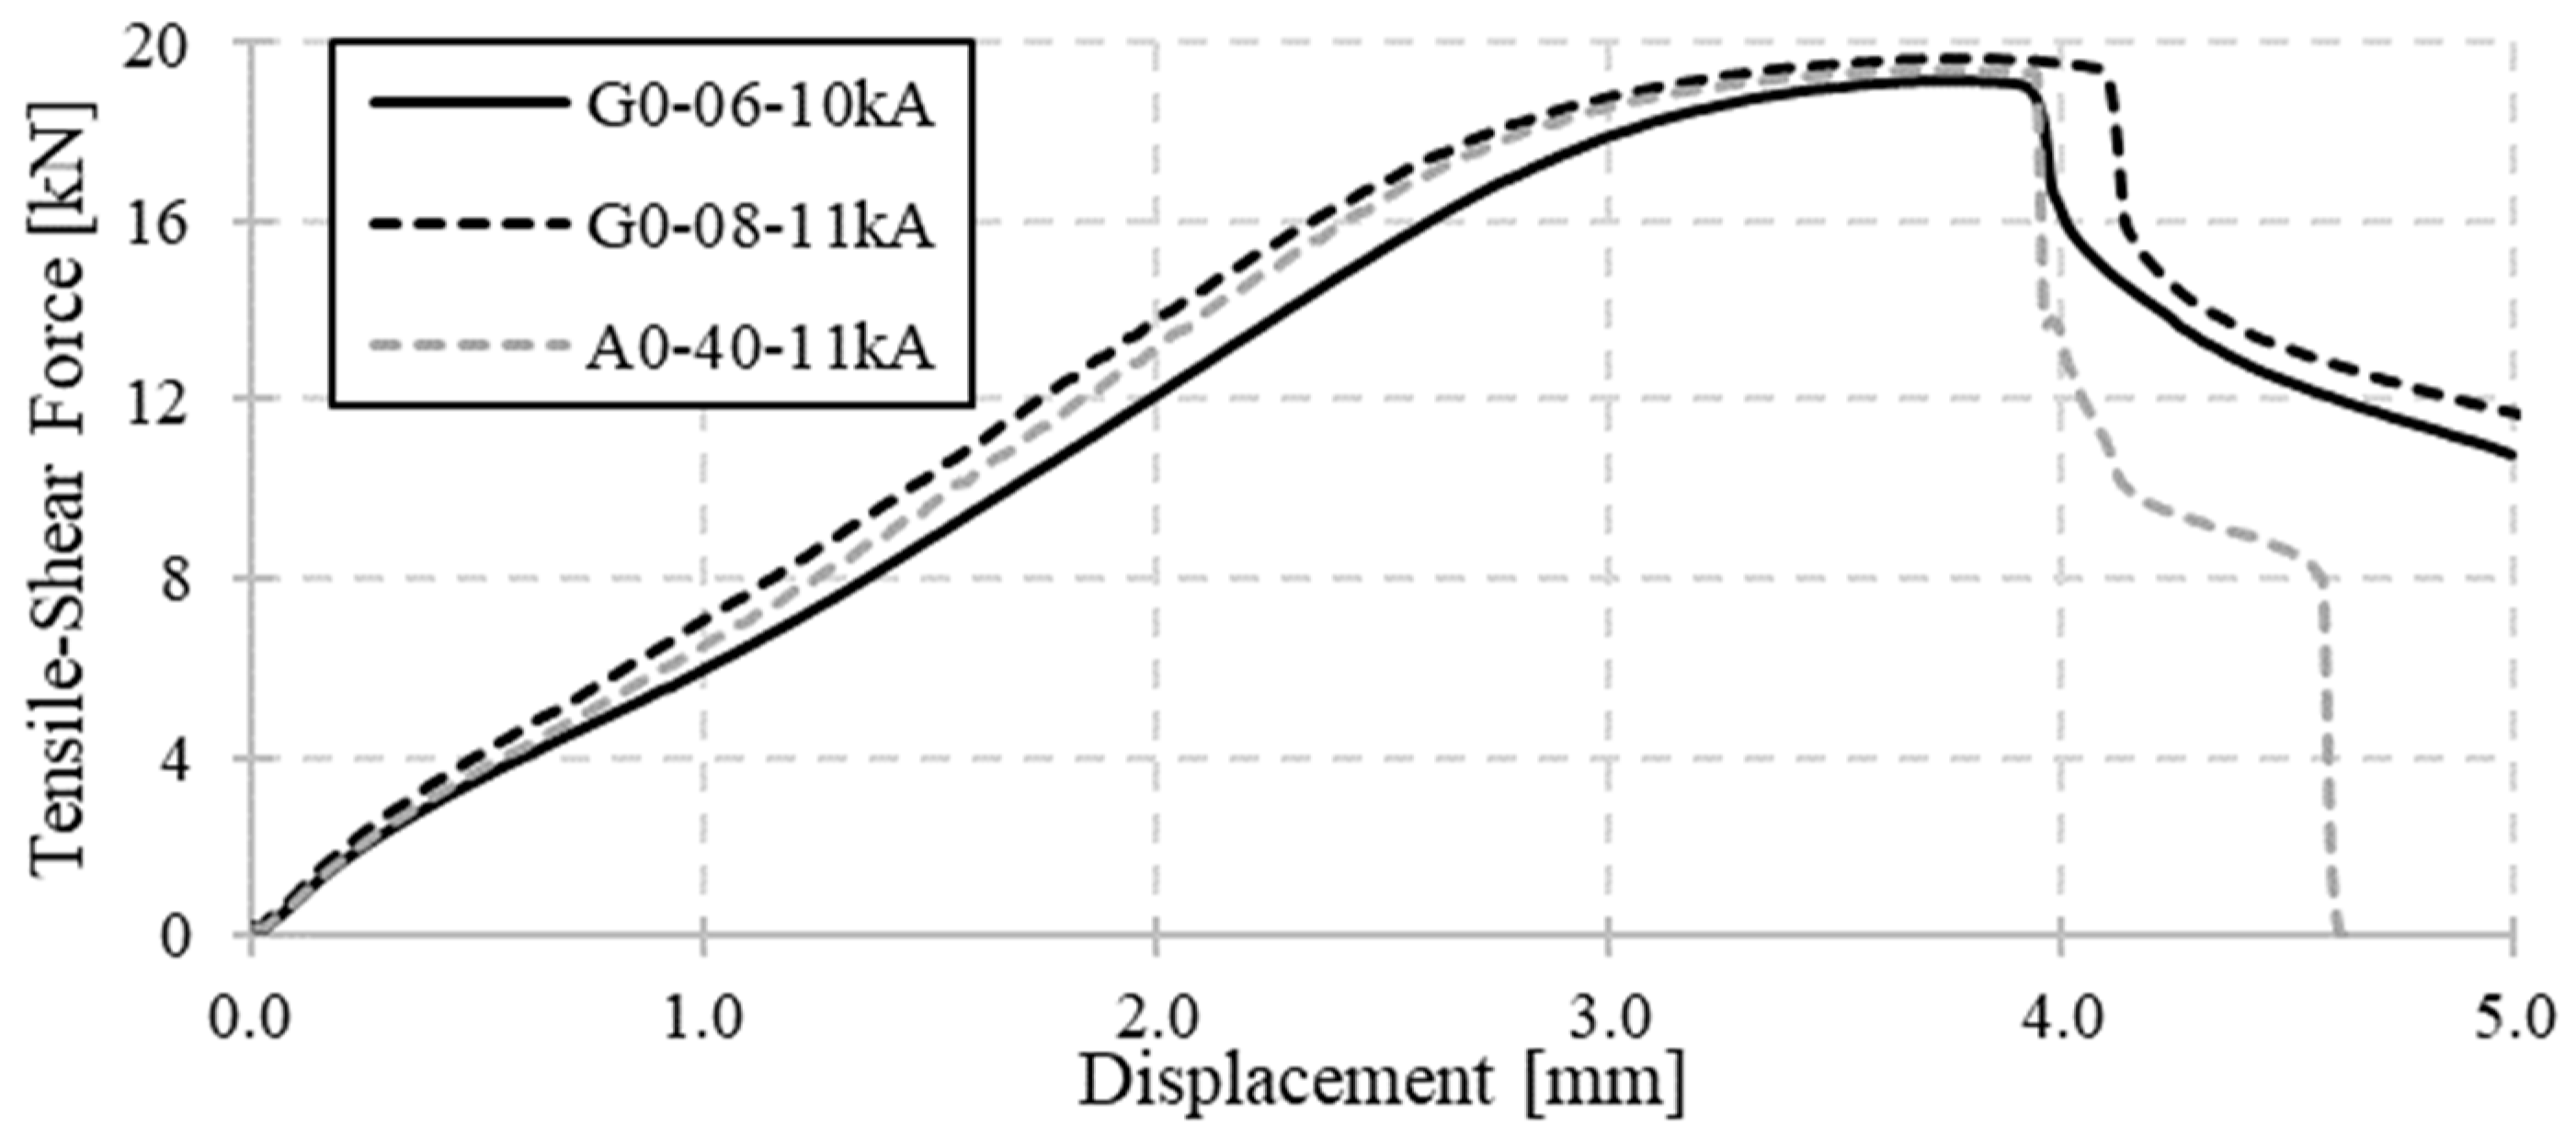
Representative tensile-shear load versus displacement curves of the joints produced using different electrode geometries and welding currents are presented in Figure 7. In all cases, the tensile-shear load increased almost linearly up to a displacement of approximately 3.0 mm. Between displacements of 3.0 mm and about 4.0 mm, the rate of load increase gradually decreased for all electrode geometries. For the G0-06 geometry welded at 10.0 kA and the G0-08 geometry welded at 11.0 kA, the decrease in load after reaching the maximum value was relatively smooth, indicating that the joints did not fail in a brittle manner. In contrast, for the A0-40 geometry welded at 11.0 kA, the drop in load following the peak was noticeably sharper compared to the other cases.
Figure 7.
Representative tensile-shear force versus displacement curves of selected electrode geometry and welding currents.
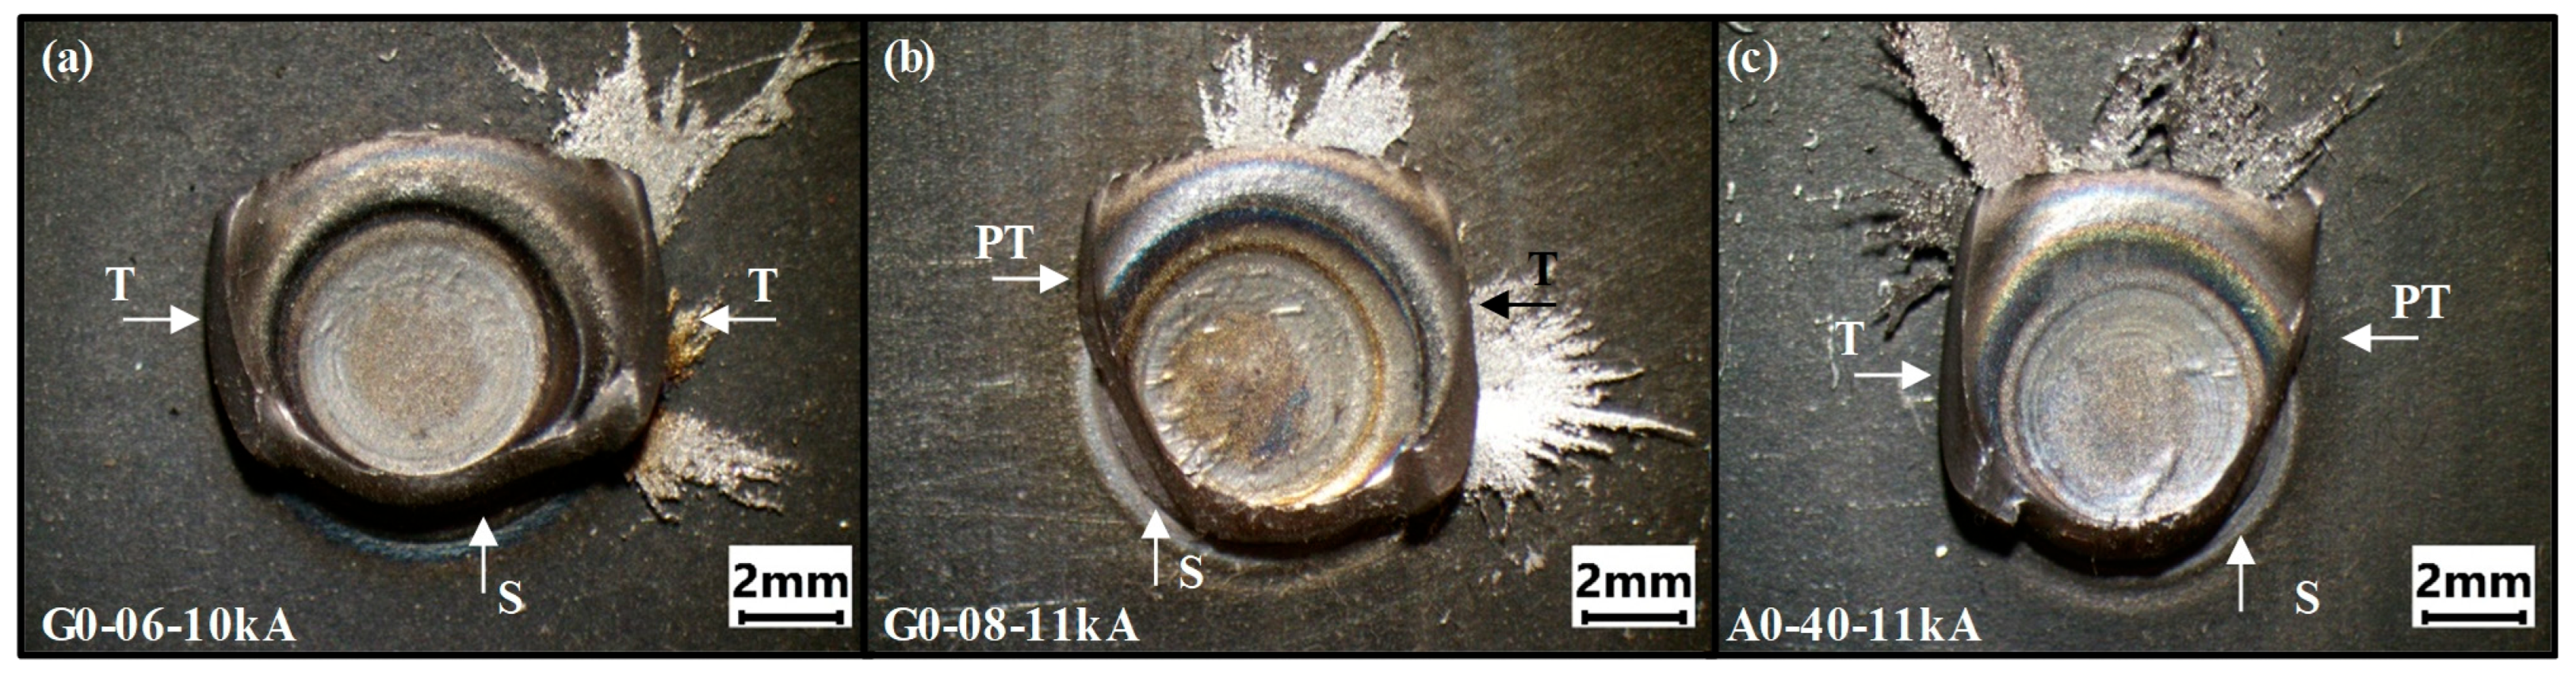
The tensile-shear force versus displacement behavior observed in Figure 7 can be explained by the fracture types shown in Figure 8. First of all, it should be noted that in all examined cases, a small amount of expulsion occurred during welding. For the joint produced using the G0-06 electrode geometry at a welding current of 10.0 kA, the fracture process occurred in two stages. First, a shear fracture formed beneath the weld nugget along the sheet thickness direction, followed by a tearing fracture in the SPFC590 sheet near the sides of the nugget region. This two-step fracture mechanism explains the gradual decrease in load after the maximum tensile-shear force observed in Figure 7. A similar failure pattern was also detected for the G0-08 electrode geometry welded at 11.0 kA, where the joint exhibited a two-stage fracture consisting of an initial shear fracture beneath the nugget and subsequent tearing along the SPFC590 sheet. In contrast, for the A0-40 electrode geometry welded at 11.0 kA, the extent of tearing following the shear fracture was limited. As shown in Figure 8, this tearing was confined to the partially left side of the nugget region. Consequently, the load drop after the maximum force in Figure 7 occurred more rapidly compared to the other conditions. As a result, although the tensile-shear strength values obtained with the A0-40 electrode were relatively high, the corresponding failure energy values were lower, particularly when compared to the G0-08 electrode geometry.
Figure 8.
Representative fracture surfaces of RSW joints generated using (a) G0-06 electrode and 10.0 kA current, (b) G0-08 electrode and 11.0 kA current, and (c) A0-40 electrode and 11.0 kA current (Shown flat sheets are MS1500 steel, pull-out combined with material tear occurred in SPFC590 steel). (S stands for shear lip, T stands for tear ridge, and PT stands for partial tear ridge).
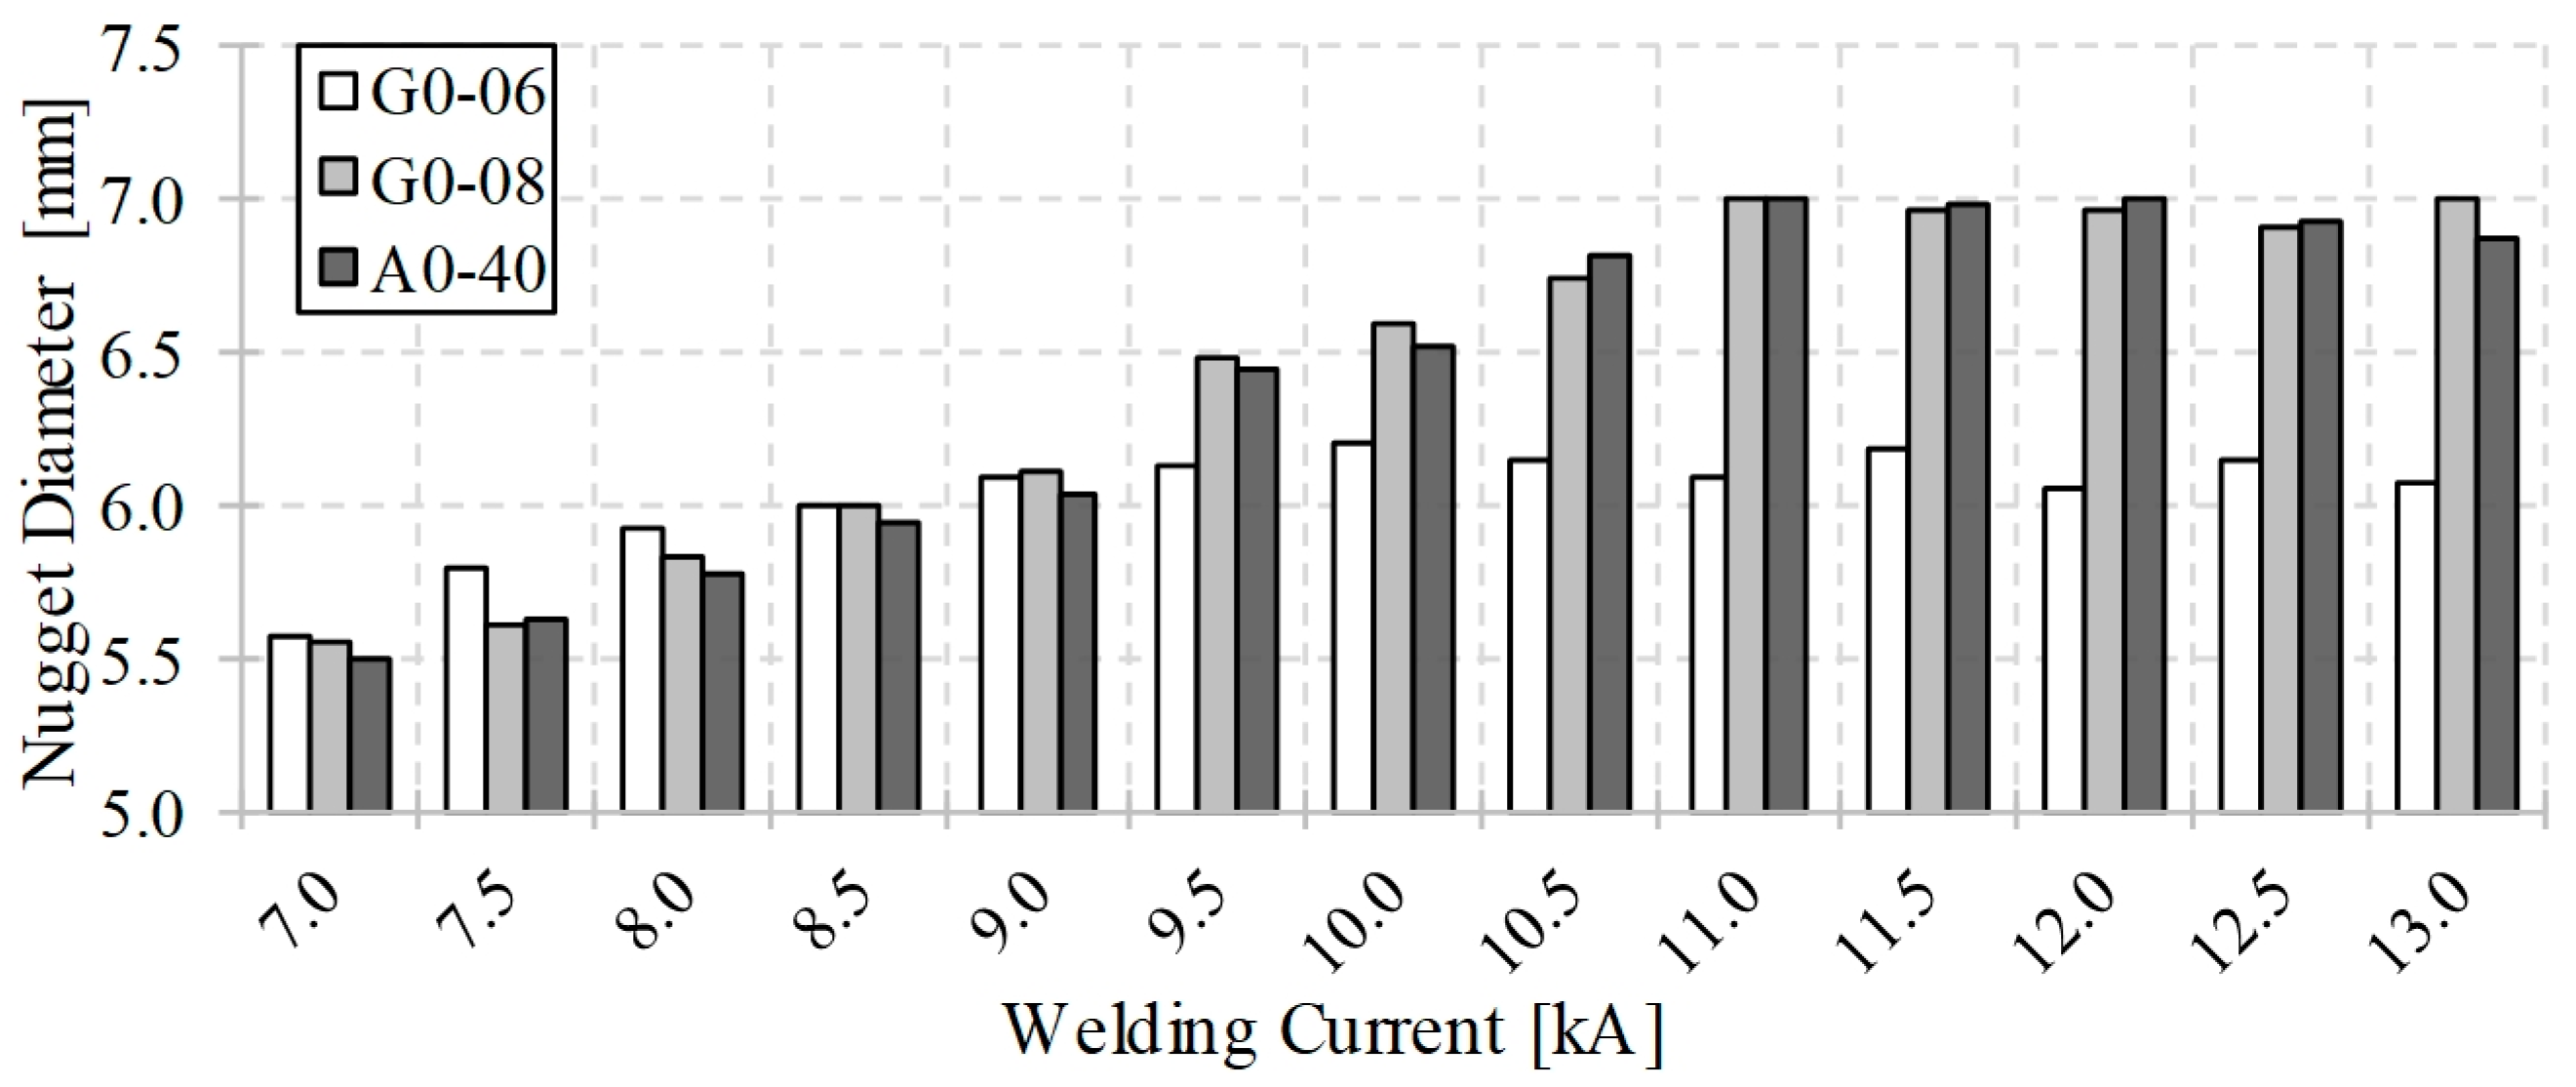
The nugget diameter values measured in the cross-sections of the joints produced with different electrode geometries and welding currents are presented in Figure 9. At a welding current of 7.0 kA, the nugget diameters obtained for all electrode geometries were nearly identical, which corresponds well with the similar tensile-shear strength and failure energy values shown in Figure 5 and Figure 6. As the welding current increased, the nugget diameter values also increased. Up to a current of 9.0 kA, the growth rate of the nugget diameter was higher for the G0-06 electrode geometry compared to the others, which can be attributed to its smaller contact area and consequently higher current density. Between 9.0 kA and 11.0 kA, a more pronounced increase in nugget diameter was observed for the G0-08 and A0-40 electrode geometries. For the G0-06 geometry, the maximum nugget diameter was reached at a welding current of 10.0 kA, after which no further increase occurred even when the current was raised. A similar trend was noted for the G0-08 and A0-40 geometries beyond 11.0 kA, where the nugget diameter values remained almost constant despite higher welding currents.
Figure 9.
Nugget diameters depending on the electrode geometry and welding current.
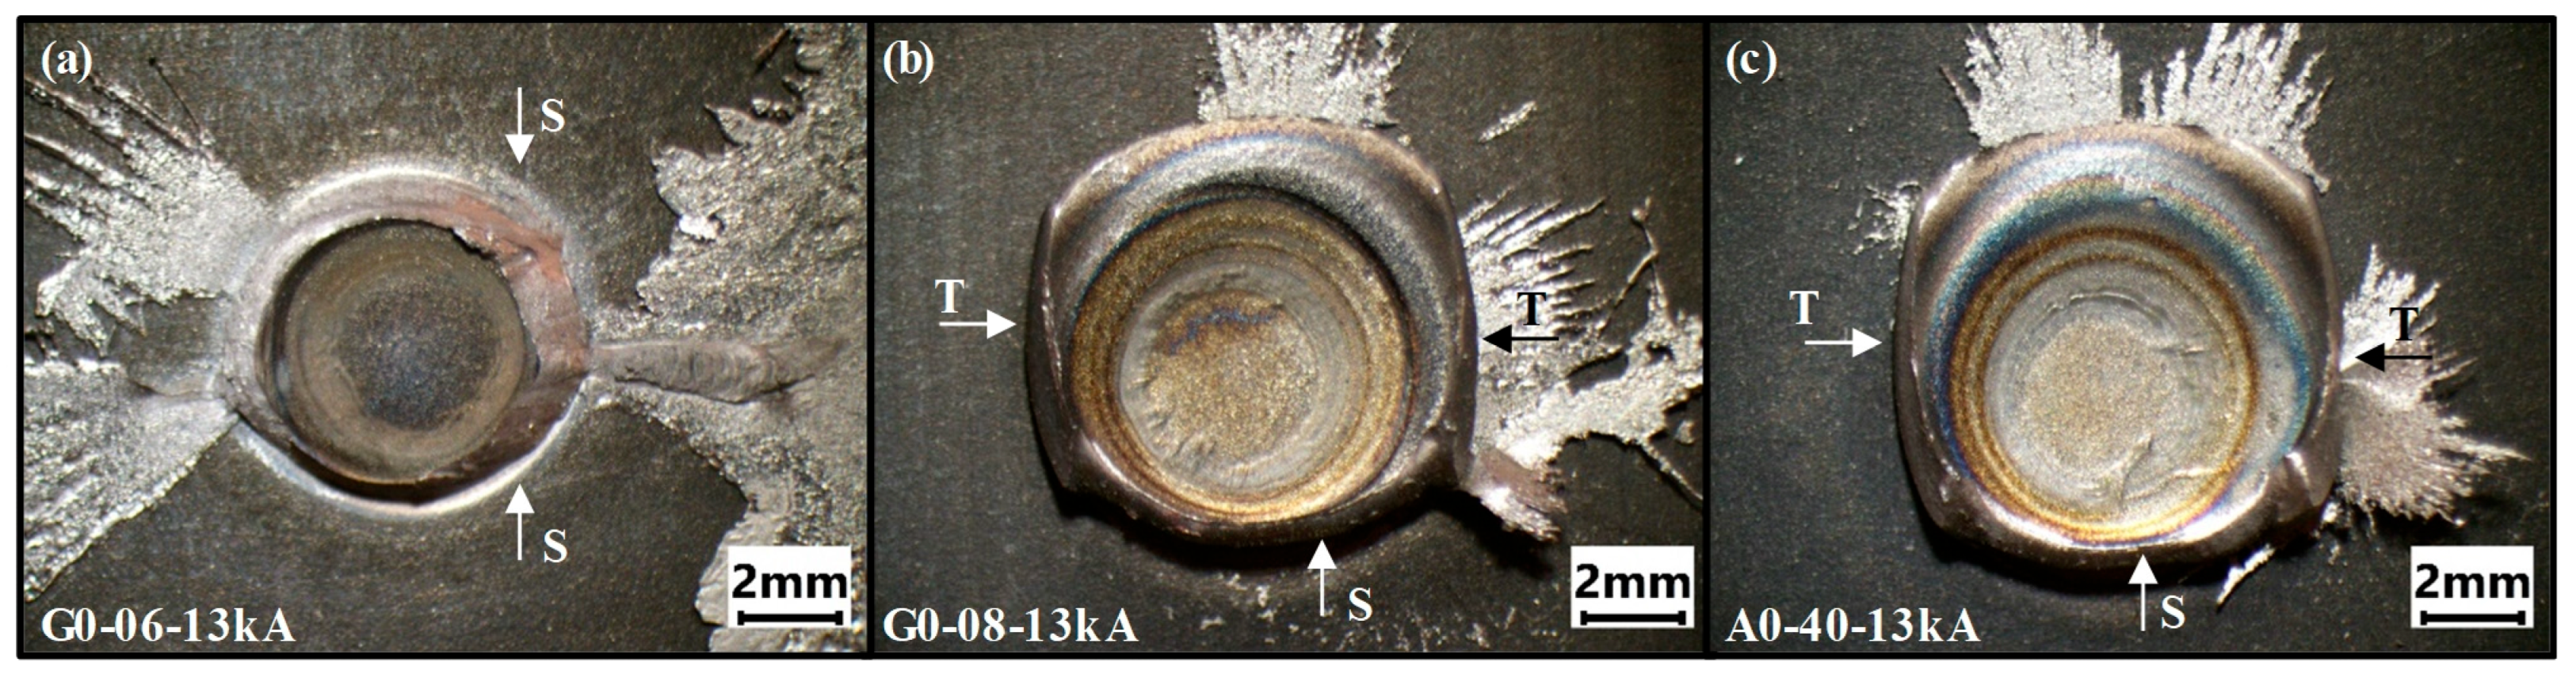
The absence of further increase in tensile-shear strength and failure energy values beyond a certain welding current level, as shown in Figure 5 and Figure 6, can be attributed to the formation of excessive expulsion during welding. The occurrence of expulsion leads to a local loss of molten material and a reduction in the effective nugget size, thereby limiting the achievable joint strength. The fracture surfaces of the joints produced at a welding current of 13.0 kA are presented in Figure 10 to illustrate the influence of excessive expulsion on the failure behavior. When using the G0-06 electrode geometry, excessive expulsion was observed at current levels higher than 10.0 kA. This behavior can be explained by the relatively small contact area of this electrode, which results in a higher current density compared to the other geometries. In addition, the smaller contact surface leads to a reduced clamping area between the electrodes, thereby increasing the likelihood of localized overheating and molten metal ejection. Consequently, excessive expulsion occurred at lower nugget diameter values for the G0-06 geometry compared with the other electrode configurations.
Figure 10.
Representative fracture surfaces of RSW joints generated using a welding current of 13.0 kA and electrode geometry of (a) G0-06, (b) G0-08, and (c) A0-40. (S stands for shear lip, and T stands for tear ridge).
In contrast, for the G0-08 and A0-40 electrode geometries, noticeably more expulsion was observed at welding currents of 11.5 kA and above compared to 11.0 kA. However, the extent of expulsion remained lower than that observed for the G0-06 geometry. This difference can be attributed to the relatively larger contact area between the electrodes and the sheet materials in the G0-08 and A0-40 geometries, which limits the current density and thus reduces the tendency for excessive expulsion formation. Nevertheless, generated expulsion was still significantly higher than the ones shown in Figure 8.
The fracture surface morphologies of the joints produced at a welding current of 13.0 kA are shown in Figure 10. In all samples, traces of molten metal ejection and localized surface depressions were visible around the nugget periphery, confirming the occurrence of excessive expulsion during welding. The G0-06 electrode geometry exhibited the most pronounced surface damage, with evident metal loss and irregular crater-like features near the nugget edge. For the G0-08 and A0-40 electrode geometries, the expelled material was comparatively limited, and the surface remained more uniform, although minor splashing marks were still present. These observations support the conclusion that increasing welding current beyond the optimal level leads to material ejection and degradation of the nugget integrity, which in turn restricts further improvement in tensile-shear strength and failure energy values. Similar results are also reported in recent studies [36].
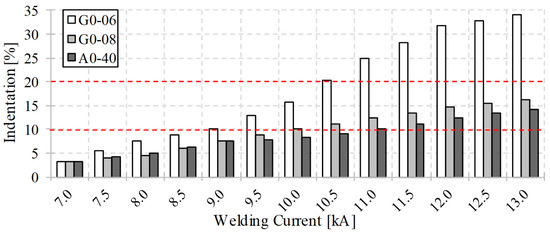
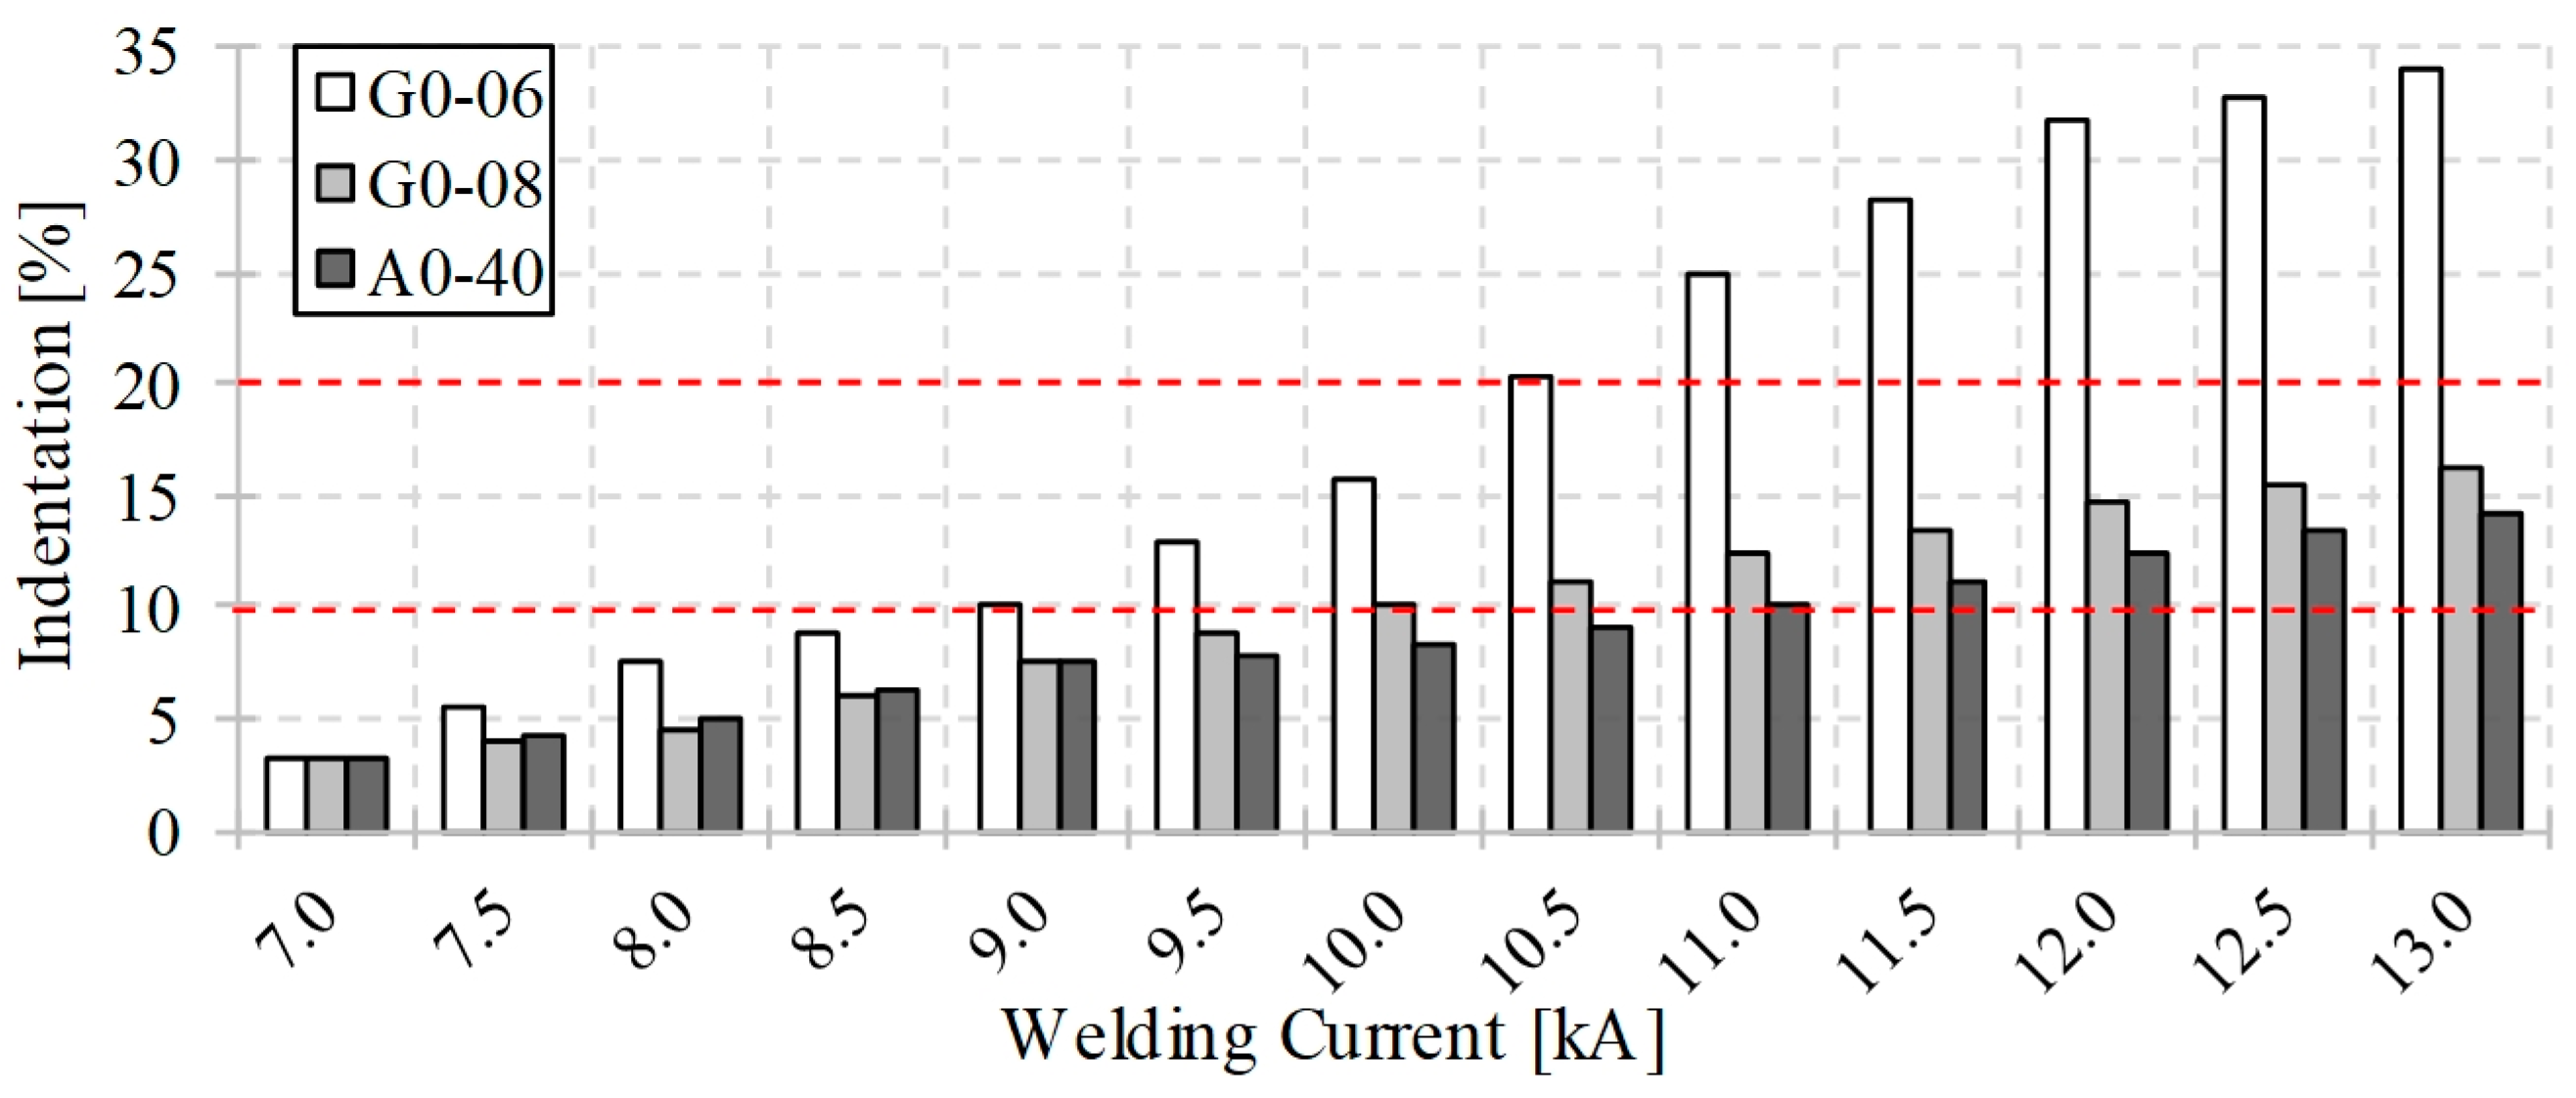
Figure 11 presents the electrode indentation values as a function of welding current and electrode geometry. In this figure, the industrially accepted indentation limits of 10% and 20% are highlighted by red dashed lines. At the lowest welding current of 7.0 kA, all electrode geometries produced nearly identical indentation values. However, when using the G0-06 electrode geometry, the indentation depth increased much more rapidly with increasing current compared to the other geometries. For this electrode type, an indentation of 15.8% was measured at 10.0 kA, where the maximum tensile-shear strength was also achieved. This value indicates that the G0-06 geometry is not suitable for welding of visible or aesthetic components. Furthermore, indentation increased sharply beyond 10.0 kA, which is also indicative of excessive expulsion during welding. In contrast, the G0-08 and A0-40 electrode geometries resulted in lower indentation levels. Since these electrodes have larger contact areas than the G0-06 type, the applied stress on the sheet surface decreases, making electrode penetration more difficult. Consequently, at the welding current of 11.0 kA—where the highest tensile-shear strength and failure energy were obtained—the indentation values were measured as 12.5% for the G0-08 geometry and 10% for the A0-40 geometry.
Figure 11.
Indentation depending on the electrode geometry and welding current.
The overall results indicate that the mechanical performance of resistance spot-welded joints is strongly governed by the combined effects of nugget growth and expulsion behavior. An increase in welding current initially promotes larger nugget formation, resulting in higher tensile-shear strength and failure energy values. However, once the nugget diameter reaches the measured saturation levels (6.59 mm for G0-06; 7.00 mm for both G0-08 and A0-40), excessive heat input leads to the onset of expulsion, causing metal loss and irregular nugget boundaries. This phenomenon explains the observed decrease or stagnation in mechanical performance at higher current levels, despite the nominal increase in welding energy. The electrode geometry also plays a crucial role in controlling current density and expulsion tendency: smaller contact areas, such as in the G0-06 geometry, accelerate nugget formation but make the process more susceptible to excessive expulsion, while larger contact areas, as in the G0-08 and A0-40 geometries, provide a more stable welding window with reduced expulsion risk. Therefore, optimizing electrode geometry in conjunction with welding current is essential for achieving a balance between sufficient nugget size and minimal expulsion to maximize joint strength and energy absorption capability.
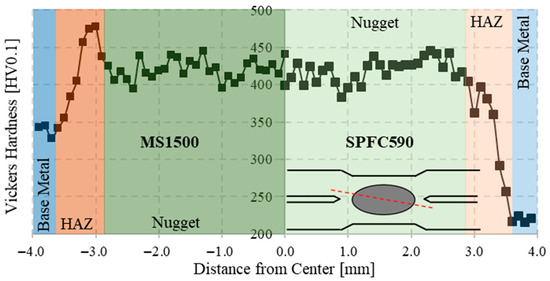
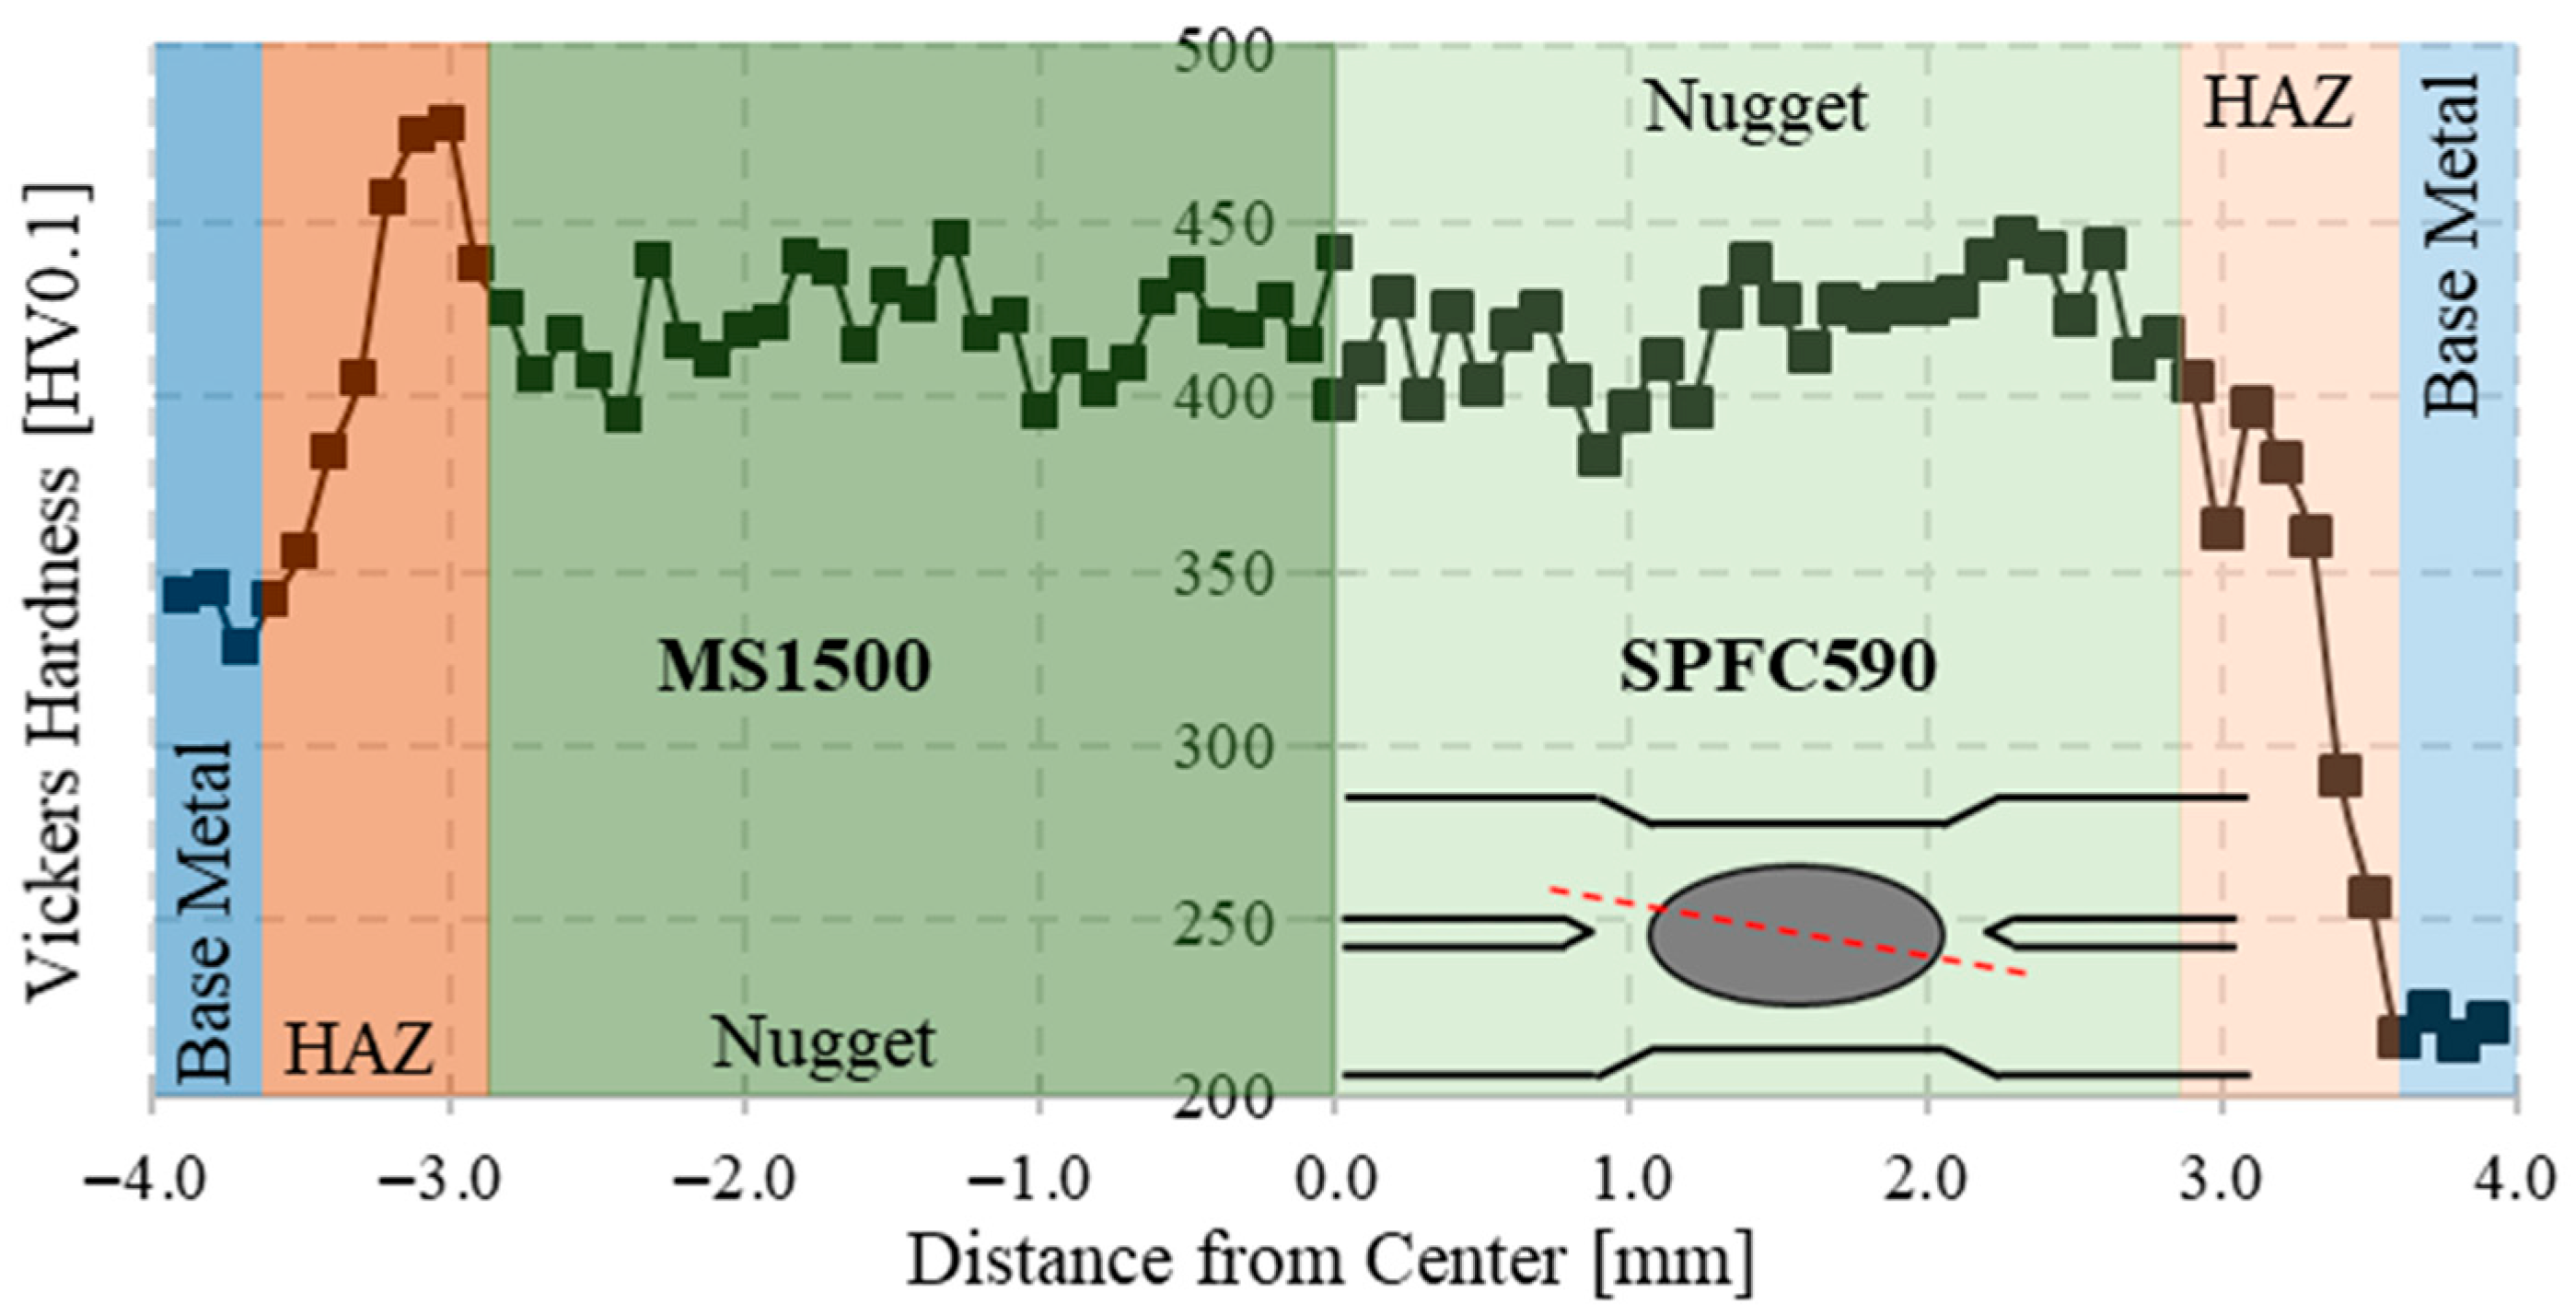
The microhardness distribution across the cross-section of the welded joint is shown in Figure 12. The presented hardness profile corresponds to the joint produced using a welding current of 11.0 kA and the G0-08 electrode geometry, which exhibited the highest mechanical strength among the investigated conditions. This specific welding condition was selected for detailed microhardness analysis because it represents the optimum combination of welding current and electrode geometry, resulting in the highest mechanical performance. The hardness measurements were performed along a line passing through the nugget center, covering the base metals, heat-affected zones (HAZ), and the nugget region of both MS1500 and SPFC590 sheets. The pictogram below the figure depicts the line along which these hardness measurements were taken. The hardness of the MS1500 base metal was significantly higher than that of the SPFC590 material due to its martensitic microstructure. The hardness levels in the base metals of MS1500 and SPFC590 were measured as 350 HV0.1 and 220 HV0.1, respectively. On the MS1500 side, a slight decrease in hardness was observed at the boundary of the HAZ region. Afterwards, when moving further into the HAZ, a noticeable hardness increase was observed in the MS1500 sheet, where the values exceeded 480 HV0.1, suggesting local phase transformation and rehardening caused by the rapid cooling following welding.
Figure 12.
Hardness distribution along the joint section.
Within the nugget region, the hardness remained relatively uniform, ranging between approximately 400 and 450 HV0.1, indicating full mixing and proper fusion of the materials. On the SPFC590 side, the hardness gradually decreased from the nugget toward the HAZ and reached its minimum in the base metal region, around 220 HV0.1. This hardness profile confirms the formation of a sound metallurgical bond, with the nugget exhibiting sufficient strength and no evidence of excessive softening in the fusion zone. Although softening in the HAZ of martensitic steels after resistance spot welding has been widely reported in the literature [15], no pronounced HAZ softening was observed in the present study. This deviation can primarily be attributed to the use of relatively thin sheet materials. The reduced sheet thickness allowed for shorter welding times and promoted rapid heat dissipation through the water-cooled electrodes, resulting in a high cooling rate of both the nugget and the HAZ. Consequently, particularly in the sub-critical HAZ, the available thermal exposure was insufficient to induce significant tempering of the martensitic microstructure, thereby preventing noticeable hardness reduction in this region.
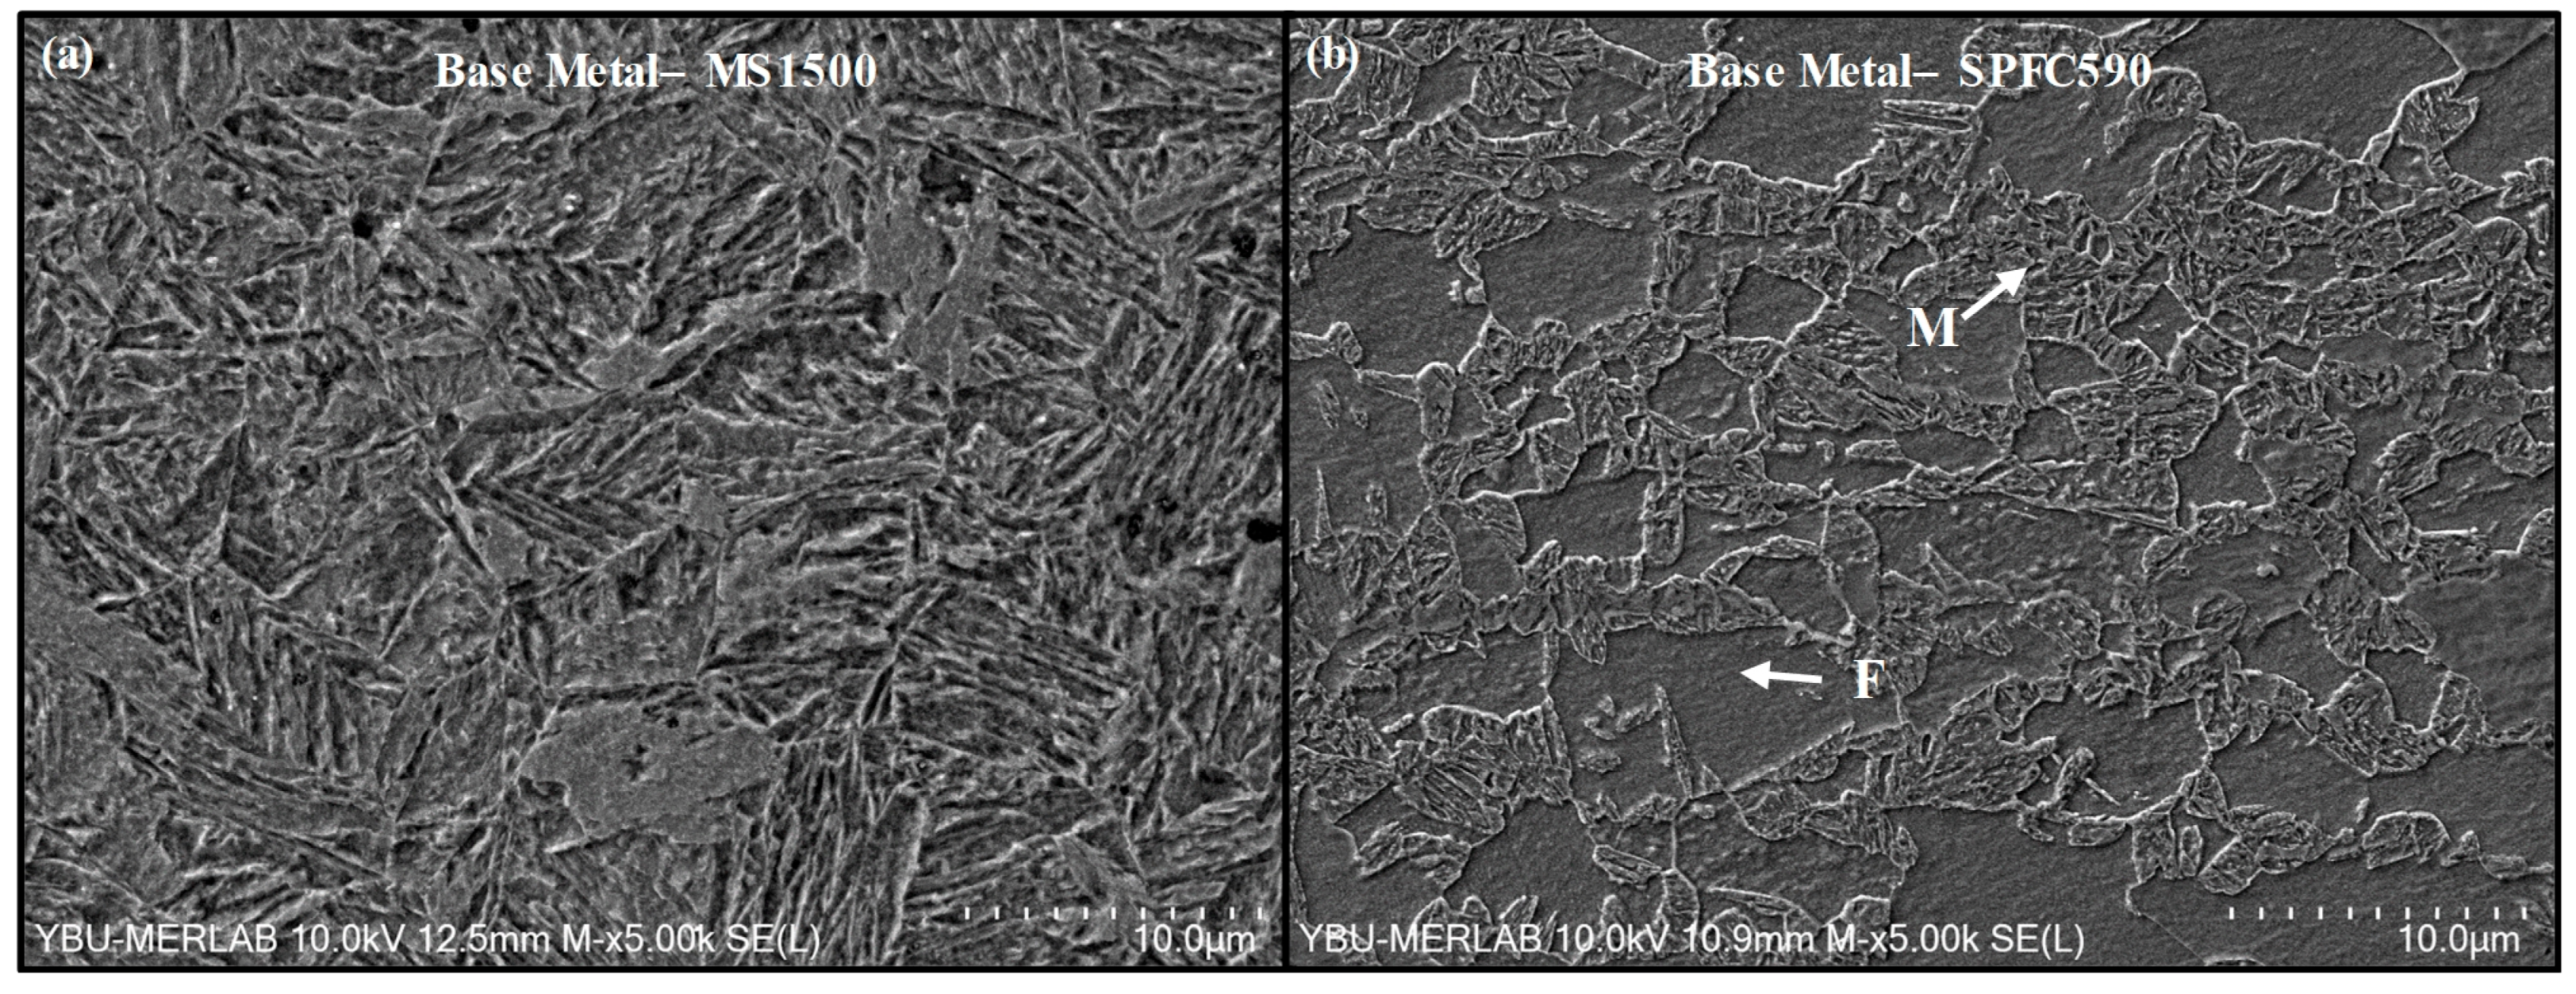
The hardness distribution results presented in Figure 12 can be explained by the characteristic microstructures. First of all, scanning electron microscopy images of the unprocessed base materials are shown in Figure 13. The microstructure of the MS1500 steel consists entirely of martensite, as clearly observed in the dendritic morphology displayed in Figure 13a. This fully martensitic structure is responsible for the high hardness and strength levels measured in both the base metal and the nugget region on the MS1500 side. In contrast, the SPFC590 material exhibits a mixed microstructure characterized by large ferritic islands containing dispersed martensitic regions, as shown in Figure 13b. This dual-phase structure explains the relatively lower hardness values observed on the SPFC590 side, while still providing the comparatively high mechanical strength values listed in Table 1.
Figure 13.
Scanning electron microscopy images of base metals in (a) MS1500 side and (b) SPFC590 side. (F stands for ferrite and M stands for martensite).
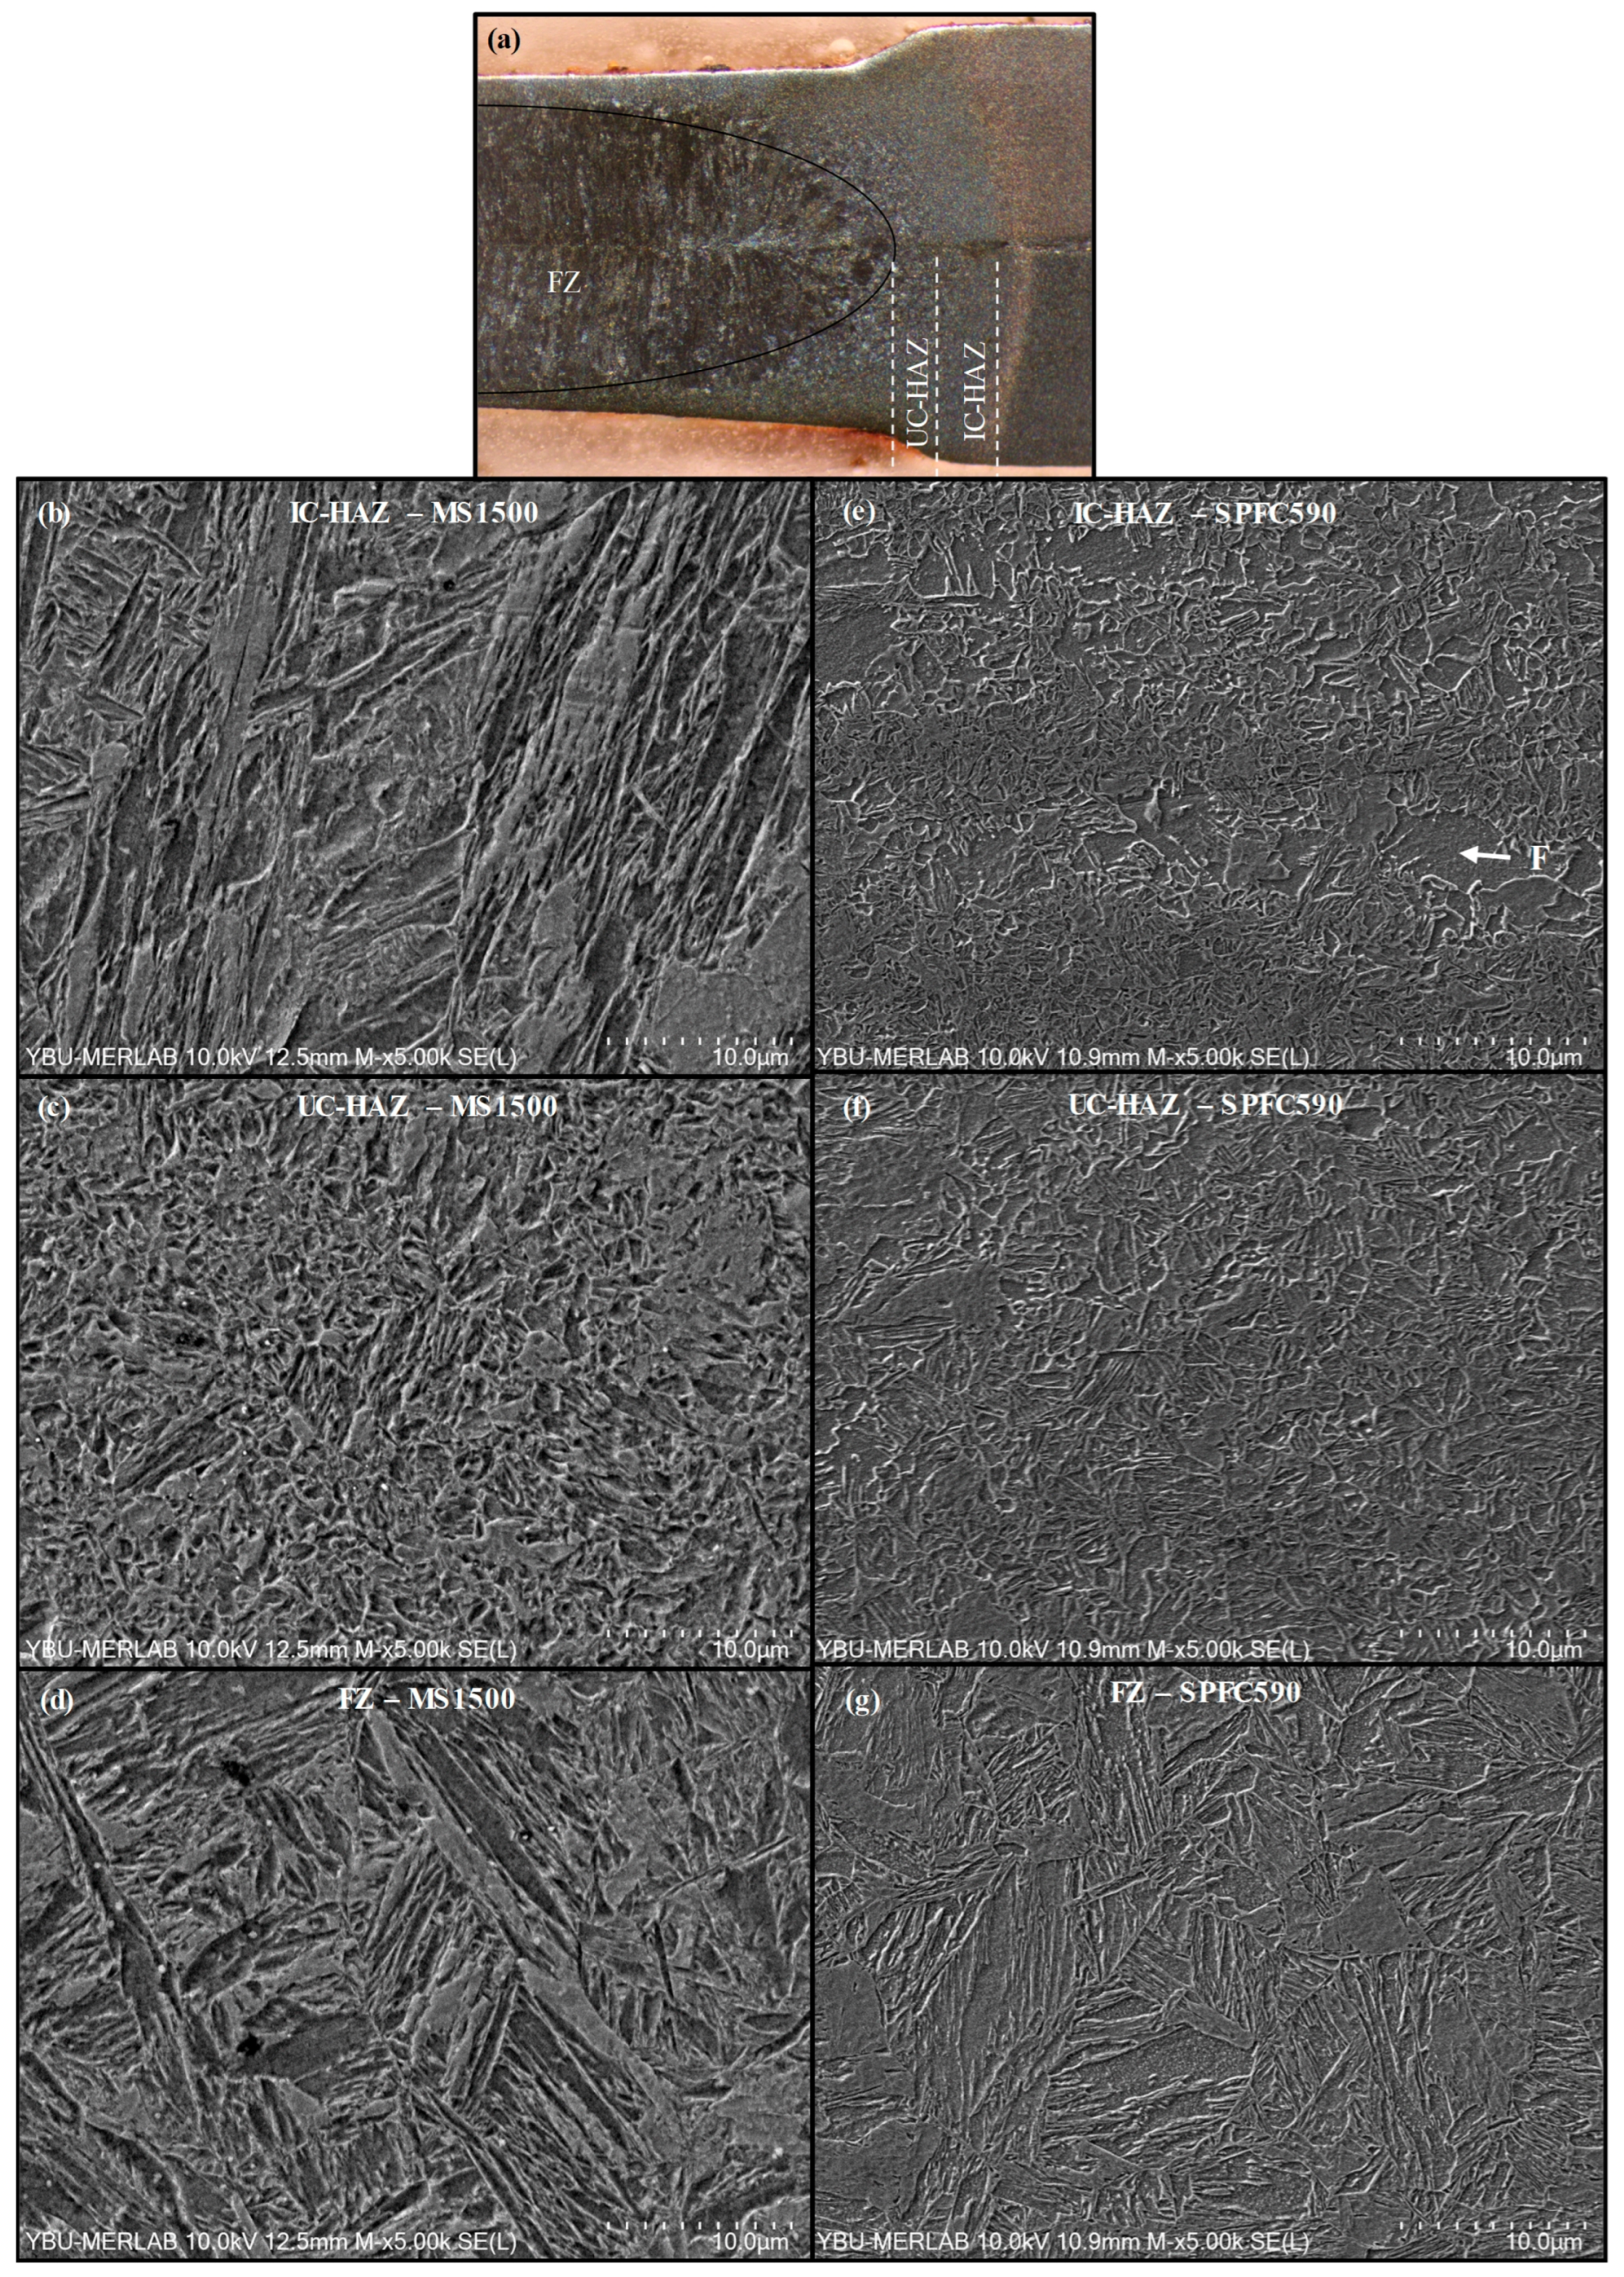
In the present study, both sheets had an identical thickness of 1.2 mm, which allowed the welding time to be limited to 12 cycles (240 ms). Owing to the low sheet thickness, heat extraction through the water-cooled electrodes was highly efficient, resulting in a very high cooling rate after current interruption. Under these conditions, the thermal exposure within the sub-critical HAZ (SCHAZ) remained insufficient to promote martensite tempering, which is typically responsible for HAZ softening in martensitic steels. As a result, no distinct microstructural features associated with a tempered martensitic structure were observed in the SCHAZ. Instead, a direct transition from the base metal microstructure (Figure 13) to the intercritical HAZ microstructures shown in Figure 14b,e was identified. Consistent with this microstructural observation, no local hardness reduction within the HAZ was detected in the hardness profile presented in Figure 12.
Figure 14.
Light microscopy (a) and scanning electron microscopy images (b–g) of (a) overall joint section (lower sheet is MS1500, upper sheet is SPFC590), (b) intercritical HAZ region of the MS1500, (c) uppercritical HAZ region of MS1500, (d) fusion zone of MS1500, (e) intercritical HAZ region of the SPFC590, (f) uppercritical HAZ region of SPFC590, (g) fusion zone of SPFC590 (F stands for ferrite).
The welding process causes noticeable changes in the microstructure shown in Figure 13. To evaluate these changes more accurately, it is necessary to examine different regions within the HAZ as well as the fusion zone separately. Figure 14 presents the microstructural features observed at several representative locations across the welded joint. First, Figure 14a illustrates the optical micrograph of the weld zone, indicating the distinct sub-regions within it. Figure 14b shows the microstructure of the MS1500 material in the intercritical heat-affected zone. When this microstructure is compared with that in Figure 13a, it can be observed that the grain size has relatively increased. In addition, due to the relatively slow cooling rate—especially because this region is located farther away from the nugget—small ferrite islands have formed within the microstructure. As a result, a decrease in hardness has been observed in the HAZ region of MS1500, as shown in Figure 12.
The microstructure of the MS1500 material in the upper critical HAZ is shown in Figure 14c. Due to its proximity to the nugget region, the temperature in this area is expected to be very high during welding, followed by rapid cooling afterward. Consequently, a noticeable grain refinement has occurred, while the martensitic microstructure has been retained. As a result, the hardness increase observed near the fusion zone in the HAZ region of the MS1500 material, as shown in Figure 12, can be attributed to this microstructural condition.
The microstructure of the MS1500 material within the fusion zone is shown in Figure 14d. In this region, a highly oriented martensitic structure, which is characteristic of the RSW process, was observed. This pronounced orientation occurs as a result of the heat flow toward the actively cooled electrodes during the holding time after the welding current is switched off. Consequently, solidification proceeds in this direction, leading to the formation of the distinctly aligned martensitic microstructure within the nugget.
The microstructure of the SPFC590 material at different regions of the weld zone is presented in Figure 14e–g. In the intercritical HAZ shown in Figure 14e, although this region is located relatively far from the nugget area, an increased amount of martensitic regions can be observed within the SPFC590 material, with ferritic islands distributed between them. Despite the lower cooling rate in this region compared to the other parts of the joint, the increase in martensite formation may be associated with the relatively high manganese content of the SPFC590 steel, which promotes hardenability and stabilizes austenite during the welding thermal cycle.
In the intercritical HAZ, illustrated in Figure 14f, the temperature locally increased between Ac1 and Ac3, leading to a partial phase transformation. Newly formed martensitic islands were observed within the ferritic matrix, contributing to a moderate increase in hardness in this region.
Finally, the fusion zone microstructure, shown in Figure 14g, exhibits a fully resolidified structure. Because this region underwent rapid solidification from very high temperatures, a fine needle-like martensitic structure was formed. This refined martensitic nugget is directly correlated with the maximum hardness observed in Figure 12.
Overall, the microstructural evolution observed across the welded joint clearly reflects the thermal gradient generated during the RSW process. The rapid heating and cooling in the nugget region resulted in the formation of a fine needle-like martensitic structure, whereas various microstructural transformations occurred within the HAZ depending on the local peak temperature. With decreasing cooling rate and maximum temperature, the martensitic structure partially transformed into tempered martensite or ferritic islands. These microstructural variations are consistent with the hardness distribution presented in Figure 12, where the highest hardness values were measured at the nugget center, followed by a distinct reduction in the heat-affected regions.
4. Conclusions
In this study, RSW joints between MS1500 and SPFC590 steels were produced using different electrode geometries and welding currents to investigate their effects on joint performance and microstructural evolution. The experimental results showed that both tensile-shear strength and failure energy increased with welding current up to an optimum level, after which further increases led to a decline due to excessive expulsion. When the G0-06 electrode geometry was used, the maximum tensile-shear strength was reached at a lower welding current of 10.0 kA compared to the other electrode geometries, and a similar trend was observed for the failure energy values. Under this condition, the highest tensile-shear strength and failure energy achieved with the G0-06 electrode were measured as 19.68 kN and 38.13 J, respectively. However, for welding currents above 10.0 kA, a pronounced decrease in both tensile-shear strength and failure energy was observed for the G0-06 electrode geometry. In contrast to G0-06, both G0-08 and A0-40 electrode geometries exhibited their maximum mechanical performance at a welding current of 11.0 kA, where the highest tensile-shear strength values of 19.28 kN and 19.68 kN were obtained for G0-08 and A0-40, respectively. When failure energy was considered, values of 43.81 J and 40.94 J were measured for G0-08 and A0-40 electrode types, respectively. This indicates that the failure energy achieved with the G0-08 electrode was approximately 7% higher. The earlier attainment of maximum mechanical strength at lower welding currents for the G0-06 electrode can be attributed to the higher current density resulting from its smaller electrode tip diameter, which promotes rapid melting within a localized area even at relatively low currents. Nevertheless, once the mechanically optimal condition is exceeded, the relatively high current density in the G0-06 geometry intensifies expulsion, leading to a sharp deterioration in mechanical performance. In contrast, the G0-08 and A0-40 electrode geometries, which have comparable contact areas with the welded sheets, require relatively higher welding currents to achieve peak mechanical properties. Owing to their lower current density compared to the G0-06 electrode, the expulsion effect remains more limited, and the reduction in mechanical performance beyond the optimal welding current is less pronounced.
The analysis of nugget formation revealed that the nugget diameter increased with rising current but reached a saturation point beyond which excessive expulsion restricted further growth. For the G0-06 electrode geometry, the largest nugget diameter was measured as 6.21 mm at a welding current of 10.0 kA, which corresponds to the condition yielding the highest mechanical strength. This behavior can be attributed to the relatively small contact area between the electrode and the sheet material in this geometry, which inherently limits the extent of the molten zone despite the high current density. In contrast, for both the G0-08 and A0-40 electrode geometries, which possess very similar contact areas with the sheet material, the maximum nugget diameter was measured as 7.00 mm when a welding current of 11.0 kA was applied. Furthermore, for all investigated electrode geometries and welding current levels, the measured nugget diameters were found to exceed the minimum required value of 5.48 mm calculated using the commonly adopted 5 criterion for sheets with a thickness of 1.2 mm, confirming that adequate nugget formation was achieved in all cases.
Indentation results confirmed that smaller electrode contact areas promoted higher indentation and expulsion tendencies, while larger contact areas provided a more stable and controllable welding window. When the G0-06 electrode geometry was employed, an indentation level of 15.8% was measured at the welding current of 10.0 kA corresponding to the maximum mechanical strength. This value exceeds the commonly accepted indentation limit of 10% for cosmetically visible components; however, it indicates that the G0-06 electrode geometry can be safely utilized in non-cosmetic applications. For the G0-08 electrode geometry, the indentation measured at the welding current of 11.0 kA—where the highest mechanical performance was obtained—was 12.5%. Although this value is still above the threshold typically required for cosmetic applications, it remains fully acceptable for many functional applications in the automotive industry. In contrast, compliance with the 10% indentation limit at the condition, providing the maximum mechanical strength was achieved only with the A0-40 electrode geometry, leads to the conclusion that this geometry is the most suitable option for cosmetically critical applications.
Fracture analyses indicated that the G0-06 and G0-08 geometries exhibited a two-stage failure sequence involving shear fracture followed by tearing in the SPFC590 sheet, whereas the A0-40 geometry showed more localized tearing, consistent with the steeper load drop observed in the tensile-shear curves.
Microhardness measurements across the joint revealed a strong correlation between hardness distribution and the microstructural transformations that occurred during welding. The nugget region exhibited a uniform hardness of approximately 400–450 HV0.1 due to the formation of a fine, needle-like martensitic structure. On the MS1500 side, a significant hardness increase up to 480 HV0.1 was observed in the upper critical HAZ, attributed to rehardening and grain refinement induced by rapid cooling. In contrast, a moderate hardness reduction occurred in the intercritical HAZ of MS1500, where ferritic islands formed within the martensitic matrix. On the SPFC590 side, the hardness gradually decreased from the nugget toward the base metal, consistent with its ferrite–martensite dual-phase microstructure. These hardness variations directly reflect the thermal gradients and phase transformations identified in the microstructural observations.
Overall, the findings demonstrate that electrode geometry and welding current jointly determine the current density, nugget development, expulsion behavior, and microstructural gradient across the joint, which together govern the mechanical and metallurgical performance of the welds. Optimizing these parameters is therefore essential to achieve a high-strength, defect-free joint with balanced mechanical integrity and controlled hardness distribution for reliable industrial applications.
Among the tested configurations, the G0-08 electrode geometry at 11.0 kA provided the most favorable combination of tensile-shear strength, failure energy, nugget diameter, and surface indentation, defining the optimal welding condition. Nevertheless, in applications where achieving optimal mechanical performance at lower welding currents is prioritized, the G0-06 electrode geometry represents a viable alternative due to its ability to reach peak strength at reduced current levels. Conversely, for cosmetically critical applications where surface quality is a governing criterion, the A0-40 electrode geometry is the most suitable option, as it consistently yielded the lowest indentation values among the investigated configurations. Overall, the present results establish a clear electrode selection guideline for dissimilar MS1500–SPFC590 resistance spot welding, indicating that the G0-08 geometry should be preferred when a balanced optimization of mechanical performance and process robustness is required, the G0-06 geometry offers higher current efficiency by achieving peak strength at lower welding currents, and the A0-40 geometry is the most suitable choice for cosmetically critical applications due to its superior indentation control.
Although the present study focuses on peak load, energy absorption, fracture behavior, and microstructural characteristics under quasi-static loading conditions, the fatigue performance and impact toughness of the welded joints were not within the scope of this work. Considering the critical role of resistance spot-welded joints in automotive crash safety, future studies should systematically investigate the influence of welding electrode geometry on fatigue life and impact behavior under dynamic loading conditions. Such investigations would provide a more comprehensive assessment of joint performance and contribute to the optimization of resistance spot welding parameters for safety-critical automotive applications.
Author Contributions
Conceptualization, M.O.G.; methodology, M.O.G. and Ü.T.; formal analysis, M.O.G.; investigation, M.O.G.; resources, Ü.T.; writing—original draft preparation, M.O.G. and Ü.T.; writing—review and editing, M.O.G.; visualization, M.O.G.; project administration, M.O.G.; funding acquisition, M.O.G. All authors have read and agreed to the published version of the manuscript.
Funding
This research was funded by Scientific and Technological Research Council of Türkiye (TÜBİTAK), grant number 5190043.
Data Availability Statement
The original contributions presented in this study are included in the article material. Further inquiries can be directed to the corresponding author.
Conflicts of Interest
Author Ümit Türkmen was employed by Rokeron Otomotiv A.S. The remaining author declares that the research was conducted in the absence of any commercial or financial relationships that could be construed as a potential conflict of interest.
References
- Kimchi, M.; Philps, D.H. Resistance Spot Welding: Fundamentals and Applications for the Automotive Industry, 2nd ed.; Springer Nature: Cham, Switzerland, 2023; p. 1. [Google Scholar]
- Pouranvari, M.; Marashi, S.P.H. Critical review of automotive steels spot welding: Process, structure and properties. Sci. Technol. Weld. Join. 2013, 18, 361–403. [Google Scholar] [CrossRef] [Scilit]
- Jaber, H.L.; Pouranvari, M.; Salim, R.K.; Hashim, F.A.; Marashi, S.P.H. Peak load and energy absorption of DP600 advanced steel resistance spot welds. Ironmak. Steelmak. 2017, 44, 699–706. [Google Scholar] [CrossRef] [Scilit]
- Mousavi Anijdan, S.H.; Sabzi, M.; Ghobeiti-Hasab, M.; Roshan-Ghiyas, A. Optimization of spot welding process parameters in dissimilar joint of dual phase steel DP600 and AISI 304 stainless steel to achieve the highest level of shear-tensile strength. Mater. Sci. Eng. A 2018, 726, 120–125. [Google Scholar] [CrossRef] [Scilit]
- Pouranvari, M.; Marashi, S.P.H.; Mousavizadeh, S.M. Dissimilar resistance spot welding of DP600 dual phase and AISI 1008 low carbon steels: Correlation between weld microstructure and mechanical properties. Ironmak. Steelmak. 2011, 38, 471–480. [Google Scholar] [CrossRef] [Scilit]
- Pouranvari, M.; Marashi, S.P.H. Failure mode transition in AHSS resistance spot welds. Part I: Controlling factors. Mater. Sci. Eng. A 2011, 528, 8337–8343. [Google Scholar] [CrossRef] [Scilit]
- Pouranvari, M.; Marashi, S.P.H.; Safanama, D.S. Failure mode transition in AHSS resistance spot welds. Part II: Experimental investigation and model validation. Mater. Sci. Eng. A 2011, 528, 8344–8352. [Google Scholar] [CrossRef] [Scilit]
- Zhang, H.; Senkara, J. Resistance Welding: Fundamentals and Applications, 2nd ed.; CRC Press: Boca Raton, FL, USA, 2011; p. 257. [Google Scholar]
- Kishore, K.; Kumar, P.; Mukhopadhyay, G. Resistance spot weldability of galvannealed and bare DP600 steel. J. Mater. Process. Technol. 2019, 271, 237–248. [Google Scholar] [CrossRef] [Scilit]
- Sivaraj, P.; Seeman, M.; Kanagarajan, D.; Seetharaman, R. Influence of welding parameters on mechanical properties and microstructural features of resistance spot welded dual phase steel joints. Mater. Today Proc. 2020, 22, 558–562. [Google Scholar] [CrossRef] [Scilit]
- Rao, S.S.; Chhibber, R.; Arora, K.S.; Shome, M. Resistance spot welding of galvannealed high-strength interstitial-free steel. J. Mater. Process. Technol. 2017, 246, 252–261. [Google Scholar] [CrossRef] [Scilit]
- Lu, Y.; Peer, A.; Abke, T.; Kimchi, M.; Zhang, W. Subcritical heat-affected zone softening in hot-stamped boron steel during resistance spot welding. Mater. Des. 2018, 155, 170–184. [Google Scholar] [CrossRef] [Scilit]
- Matsuda, K.; Kodama, S. Evaluation of corona bond strength of resistance spot welding. Sci. Technol. Weld. Join. 2020, 25, 66–72. [Google Scholar] [CrossRef] [Scilit]
- Pouranvari, M.; Aghajani, H.; Ghasemi, A. Enhanced mechanical properties of martensitic stainless steels resistance spot welds enabled by in situ rapid tempering. Sci. Technol. Weld. Join. 2020, 25, 119–126. [Google Scholar] [CrossRef] [Scilit]
- Pouranvari, M.; Sobhani, S.; Goodarzi, F. Resistance spot welding of MS1200 martensitic advanced high-strength steel: Microstructure–properties relationship. J. Manuf. Process. 2018, 31, 867–874. [Google Scholar] [CrossRef] [Scilit]
- Sejc, P.; Belanova, J.; Emmer, S. The structure of the welded joints between high-strength steel USIBOR 22MnB5 and mild steel H340LAD+Z140-M-B-O made by resistance spot welding. Tech. Vjesn. 2018, 25, 1052–1058. [Google Scholar] [CrossRef] [Scilit]
- Feng, Q.; Li, J.; Xie, D.; Li, Y. Effect of a single-sided magnetic field on microstructure and properties of resistance spot weld nuggets in H1000/DP590 dissimilar steels. Metals 2025, 15, 1259. [Google Scholar] [CrossRef] [Scilit]
- Yang, K.; Meschut, G.; Seitz, G.; Biegler, M.; Rethmeier, M. The identification of a new liquid metal embrittlement (LME) type in resistance spot welding of advanced high-strength steels on reduced flange widths. Metals 2023, 13, 1754. [Google Scholar] [CrossRef] [Scilit]
- Morales-Sánchez, G.; Collazo, A.; Doval-Gandoy, J. Influence of the process parameters on the quality and efficiency of the resistance spot welding process of advanced high-strength complex-phase steels. Metals 2021, 11, 1545. [Google Scholar] [CrossRef] [Scilit]
- Yuan, X.; Li, C.; Chen, J.; Li, X.; Liang, X.; Pan, X. Resistance spot welding of dissimilar DP600 and DC54D steels. J. Mater. Process. Technol. 2017, 239, 31–41. [Google Scholar] [CrossRef] [Scilit]
- Zhang, H.; Qiu, X.; Xing, F.; Bai, J.; Chen, J. Failure analysis of dissimilar thickness resistance spot welded joints in dual-phase steels during tensile shear test. Mater. Des. 2014, 55, 366–372. [Google Scholar] [CrossRef] [Scilit]
- Onar, V. Mechanical and microstructural characterizations of resistance spot welded dissimilar TWIP/304L stainless steel. Trans. Indian Inst. Met. 2022, 75, 1731–1739. [Google Scholar] [CrossRef] [Scilit]
- Özen, F.; Onar, V.; Bulca, M.; Aslanlar, S. Resistance spot weldability of Fe–15.4Mn–2.1Al–1.2C twinning-induced plasticity steel. Mater. Werkst. 2023, 54, 857–870. [Google Scholar] [CrossRef] [Scilit]
- Özen, F. Mechanical and microstructural characterization of resistance spot welded dissimilar TWIP1000/TRIP800 joints. Mater. Test. 2024, 66, 9–21. [Google Scholar] [CrossRef] [Scilit]
- Yaghoobi, F.; Jamaati, R.; Aval, H.J. Resistance spot welding of high-strength DP steel and nano/ultrafine-grained IF steel sheets. Mater. Chem. Phys. 2022, 281, 125909. [Google Scholar] [CrossRef] [Scilit]
- Chabok, A.; van der Aa, E.; Basu, I.; De Hosson, J.; Pei, Y. Effect of pulse scheme on the microstructural evolution, residual stress state and mechanical performance of resistance spot welded DP1000-GI steel. Sci. Technol. Weld. Join. 2018, 23, 649–658. [Google Scholar] [CrossRef] [Scilit]
- Wei, F.; Zhu, Y.; Tian, Y.; Liu, H.; Zhou, Y.; Zhu, Z. Resistance spot welding of dissimilar metals: Medium manganese TRIP steel and DP590. Metals 2022, 12, 1596. [Google Scholar] [CrossRef] [Scilit]
- ISO 6892-1:2019; Metallic Materials—Tensile Testing—Part 1: Method of Test at Room Temperature. International Organization for Standardization: Geneva, Switzerland, 2019.
- ISO 14273:2016; Specimen Dimensions and Procedure for Shear Testing Resistance Spot, Seam and Embossed Projection Welds. International Organization for Standardization: Geneva, Switzerland, 2016.
- AWS C1.1M/C1.1:2019; Recommended Practices for Resistance Welding. American Welding Society: Miami, FL, USA, 2019.
- Görtan, M.O.; Yüksel, B.; Çağırankaya, F. Control of the martensitic transformation during resistance spot welding of high-strength S700MC steel. Shape Mem. Superelasticity 2023, 9, 485–491. [Google Scholar] [CrossRef] [Scilit]
- ISO 5821:2025; Resistance Welding—Spot Welding Electrode—Female Electrode Caps. International Organization for Standardization: Geneva, Switzerland, 2025.
- ISO 5182:2016; Resistance Welding—Materials for Electrodes and Ancillary Equipment. International Organization for Standardization: Geneva, Switzerland, 2016.
- ISO 6507-1:2018; Metallic Materials—Vickers Hardness Test—Part 1: Test Method. International Organization for Standardization: Geneva, Switzerland, 2018.
- Görtan, M.O. Çift aşamalı nokta direnç kaynağı uygulamasının yüksek dayanım düşük alaşımlı S700 çeliğinin mekanik dayanımına etkisinin incelenmesi. J. Polytech. 2025, 28, 673–681. [Google Scholar] [CrossRef] [Scilit]
- Zhang, Z.; Chen, W.; Hu, X.; Yi, G.; Chen, B.; Wang, J.; Jiang, L.; Jiang, X.; Li, Q. Influence of temperature gradient bonding on the micromorphology and shear performance of Sn-based solder joints: Experiments and first principles calculations. J. Manuf. Process. 2024, 121, 446–460. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license.