


Abstract
Engineering parts have increasingly higher requirements for geometric accuracy and shape deviation. In 3D printing, optimal physical and mechanical properties and dimensional accuracy are often sought, as parts produced with this technology are increasingly used not only for prototypes but also for responsible technical products. This requires precise studies of 3D printing parameters of engineering filaments. Accuracy is how close the measured size is to the CAD model. Carbon fiber-reinforced polymers are characterized by high strength and stiffness. In this article, dimensional accuracy of 3D-printed parts made of carbon fiber-reinforced polyamide was studied. For this purpose, eight samples were produced in the shape of a rectangular prism with two types of through holes—hexagonal and round. The dimensional accuracy of the overall dimensions and the holes was studied. The data was processed statistically with the aim of building an adequate mathematical model that analytically synthesizes the expected dimensional accuracy for different combinations of the selected 3D-printed parameters.
1. Introduction
In recent years, 3D printing has developed dramatically, as has the field of its application. The technology is used in automotive, space technology, medicine, pharmacy, the dental industry, etc. [1,2,3]. The quality of the final product depends mainly on printing parameters [4]. In parallel with the development of technology, more and more materials are used that are characterized by high accuracy and quality. Initially used for rapid prototyping, the technology is increasingly used to produce engineering parts, tools, and other components. [5]. The use of 3D printing for highly responsible parts has increased requirements for the properties of the parts—mechanical, physical, etc. [6]. Along with them, an important characteristic of 3D-printed parts is their accuracy, especially for assembled large units [7]. Accuracy depends on both used materials and the printing parameters. Dimensional accuracy in 3D printing is characterized by the deviation of the real part from the theoretical one, i.e., from the CAD model. An integral part of dimensional accuracy is the precision or repeatability of the obtained dimensions within a certain variation [8].
The most common materials for 3D printing are ABS, PLA, PETG, etc. [9]. Carbon fiber-reinforced plastics are extremely strong and lightweight materials. They may be considered as a highly promising material [10].
2. Materials and Methods
Carbon fiber-reinforced polyamide is a filament for 3D printing. It is characterized by high stiffness, heat resistance and adhesion. It is used for bearings and other machine elements.
The purpose of this study is to determine the accuracy of a dimensional chain in 3D printing with this material. It must be proven to what extent this material can be used for engineering tasks.
Preliminary planning was carried out using the Taguchi method in the following steps [11]:
1. Determining the goal or, more precisely the target value (dimensional accuracy) for the process.
2. Determining the parameters of the experiment planning. Two factors were selected for this material. The first factor is the 3D printing speed, marked in figures with the index X1, and the second factor is the height of the print layer, marked in figures with the index X2. Levels were set within the permissible limits for the used 3D printer model Adventurer 5M Pro manufacturer Leap3D Limited, Hong Kong, China. Printing temperature is not included in the listed factors because the material requires a minimum extrusion temperature of 280 °C, which is the maximum for this model of 3D printer.
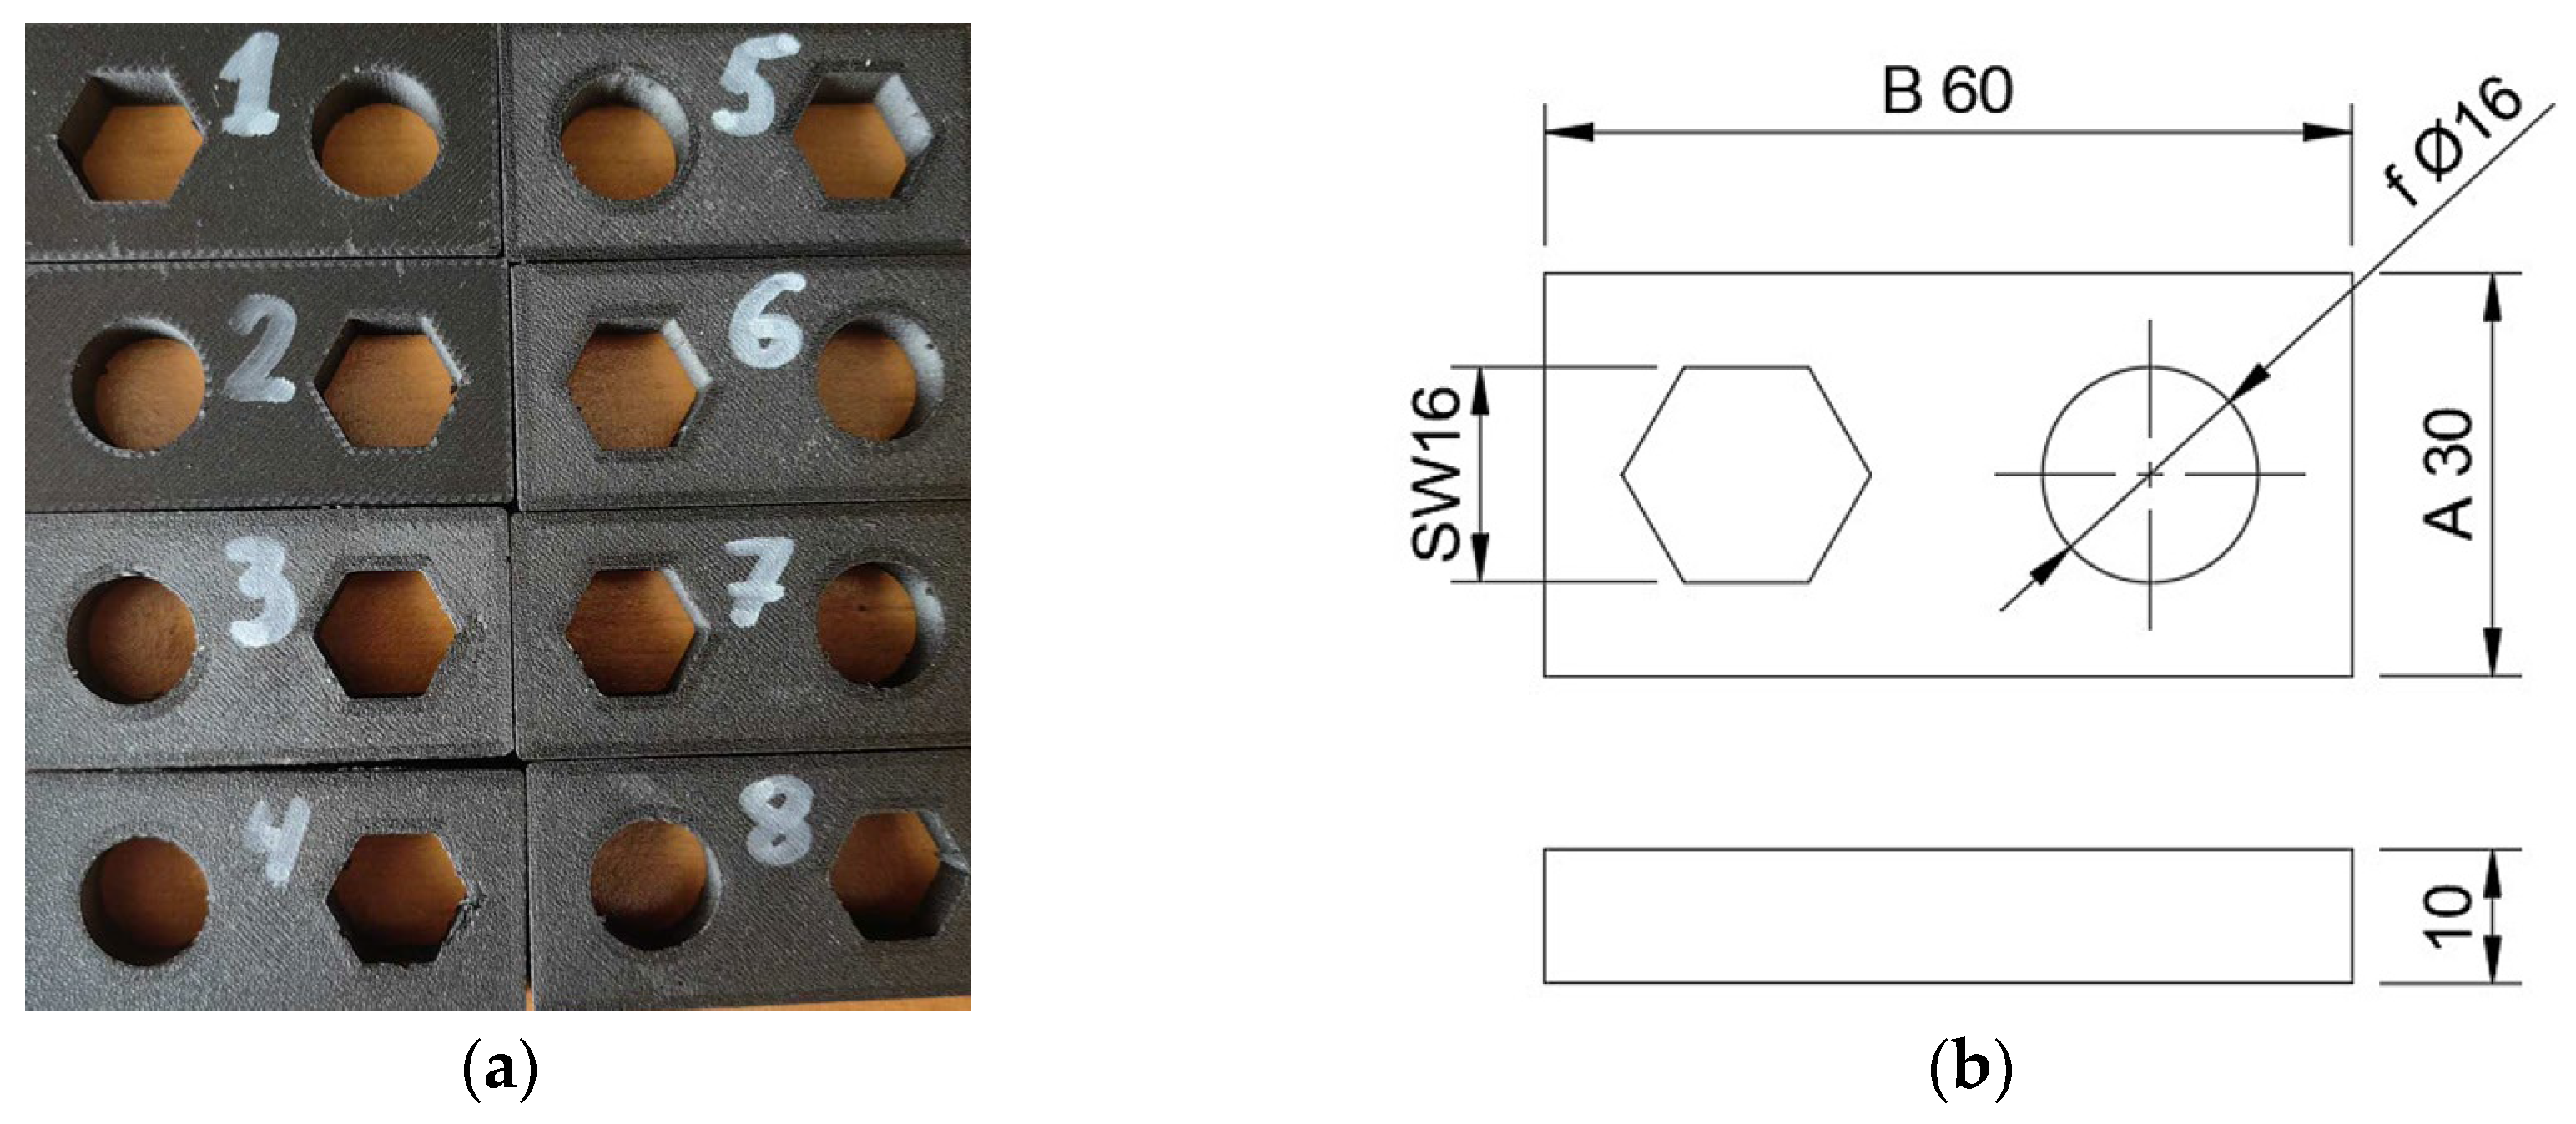
The parameters used when printing the samples shown in Figure 1 are as follows:
- Material: Polyamide PA6-CF Carbon;
- Printing speed range: 10–100 mm/s;
- Extruder temperature range: 280 °C;
- Bad temperature: 105 °C;
- Layer height range: 0.15–0.4 mm;
- Infill: 10%;
- Number of wall layers: 2 pieces;
- Flow: 83%.
Figure 1.
(a) Test specimens; (b) Dimensions of the samples.
3. Creating an orthogonal array showing the number and conditions for each experiment. Preliminary planning was performed in Minitab version 5.4, and an orthogonal array was created as shown in Table 1.
Table 1.
Printing parameters of the samples.
4. Conducting the experiments specified in the completed orthogonal array and collecting data on the effect on the target. 8 samples of Polyamide PA6-CF were printed. Figure 1b shows a drawing of the sample with the designation of the control dimensions.
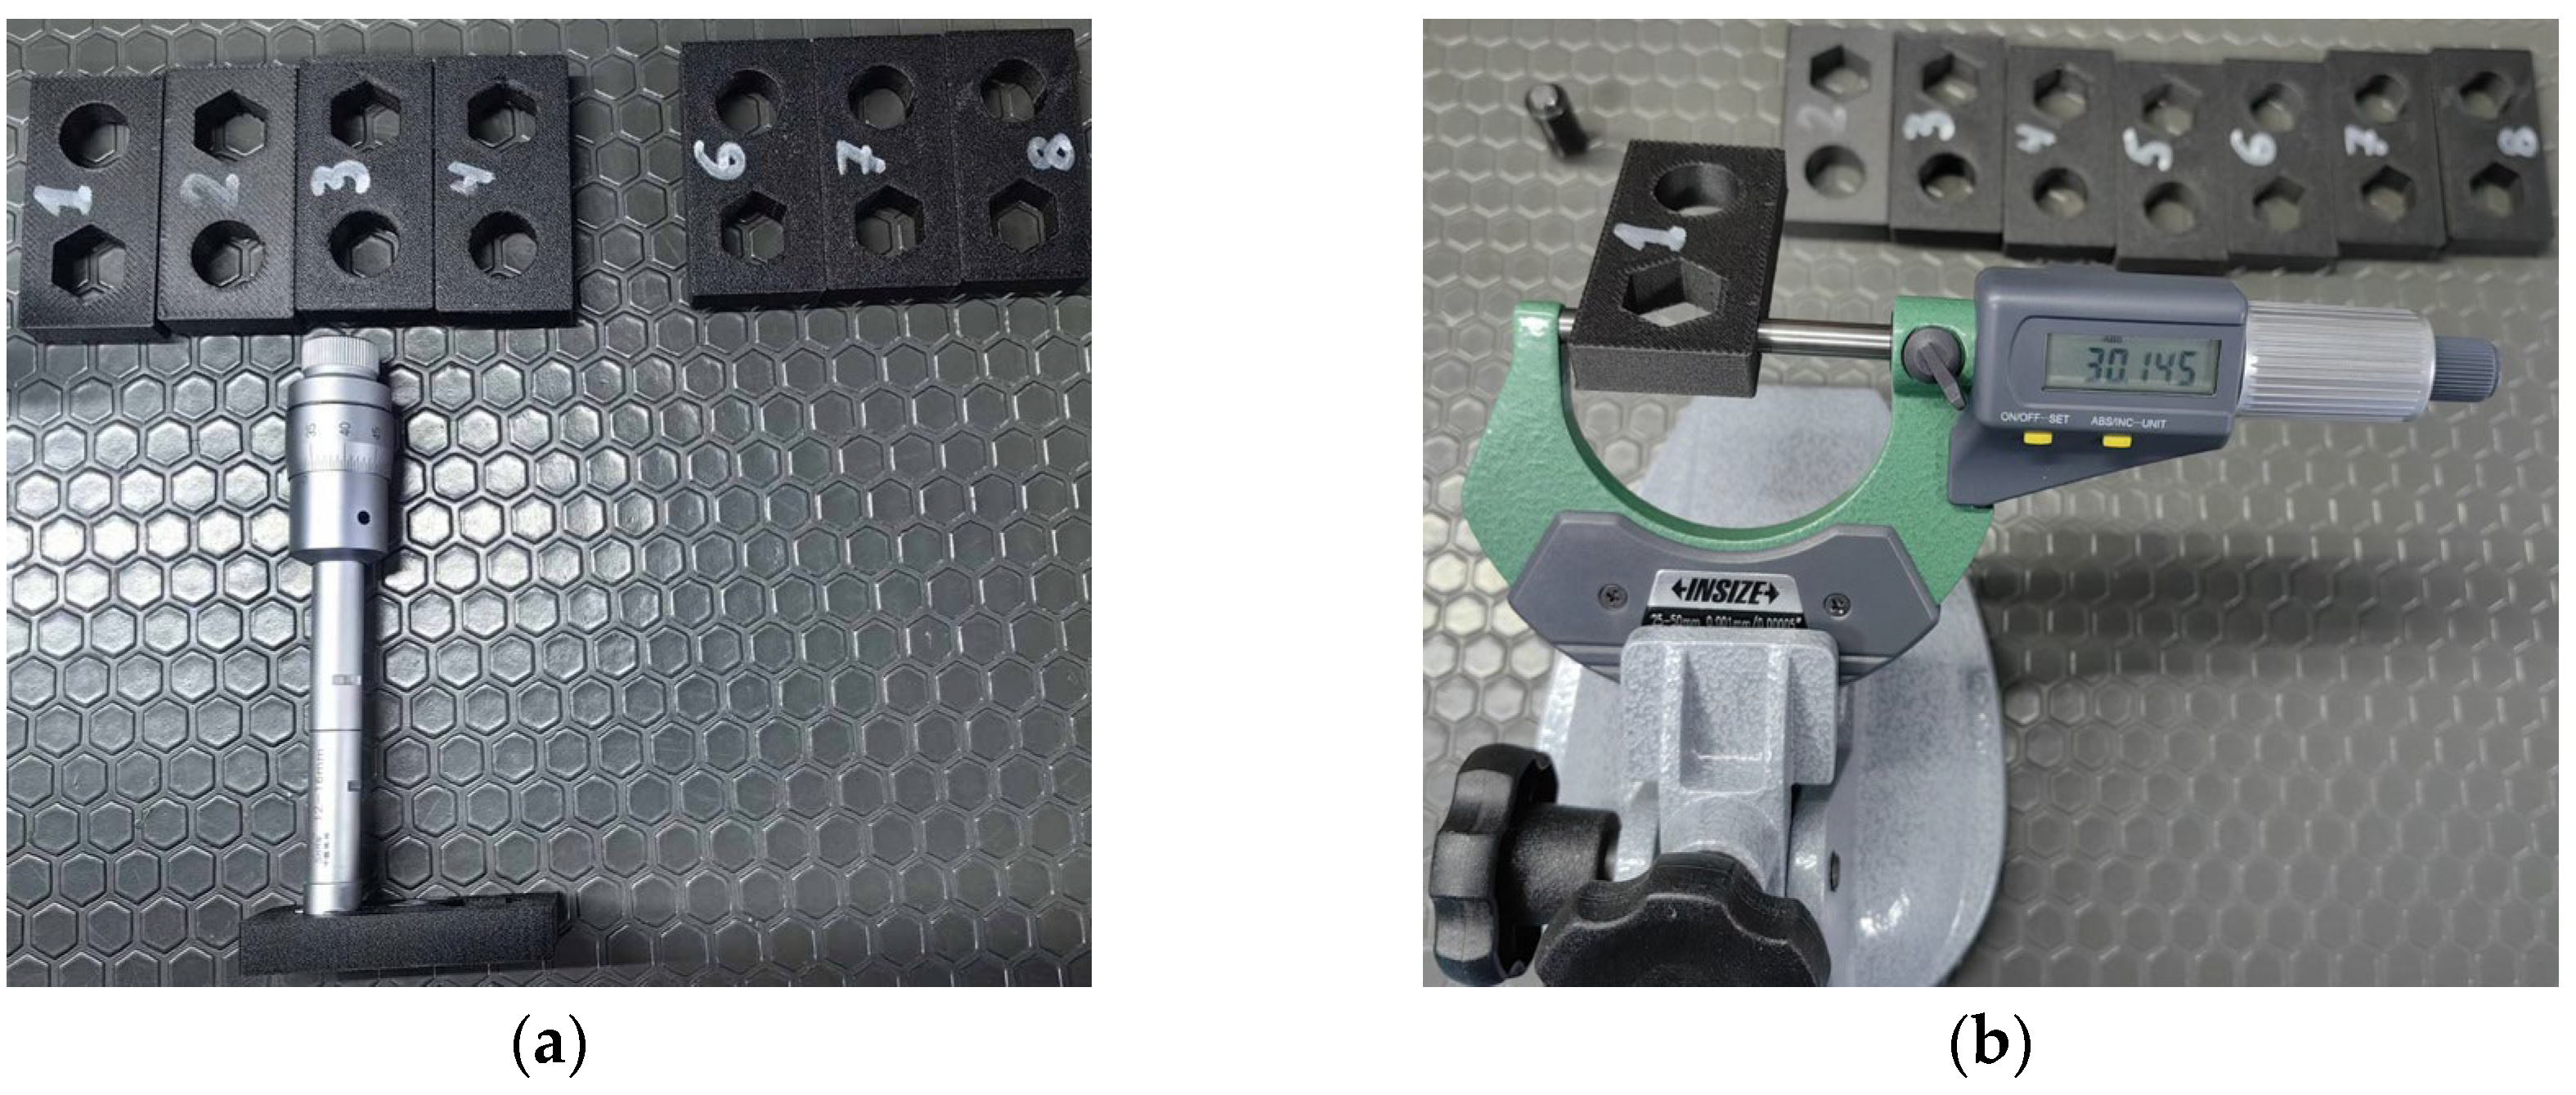
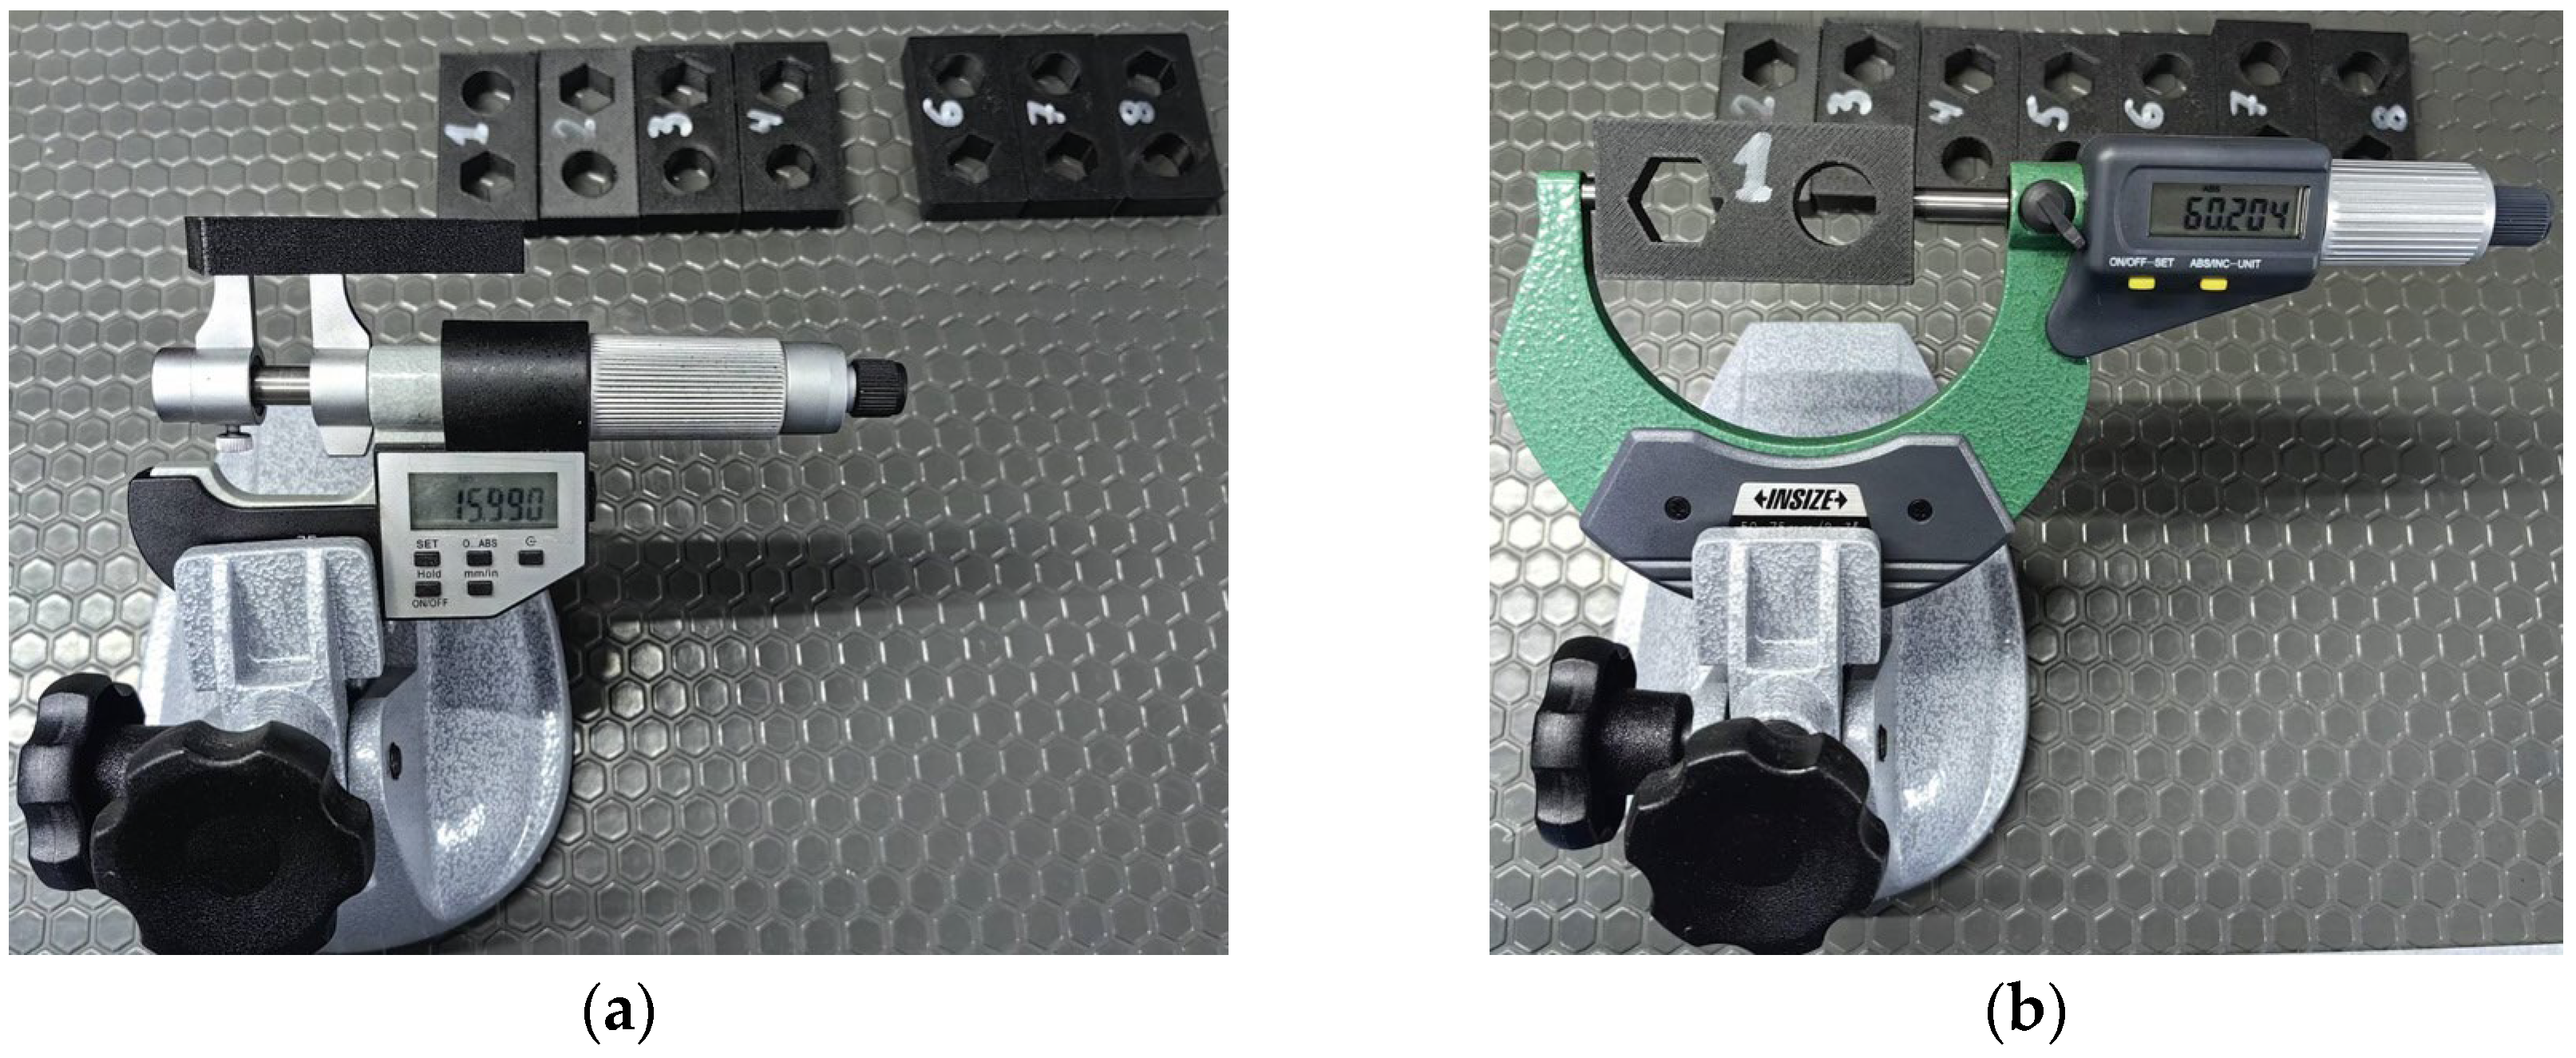
5. Measurement of the test specimens, using micrometers manufacturer Insize Europe S.L., Derio, Spain, with a resolution of 0.01 mm. The hole marked “f” with a size of φ16 mm, the hexagonal SW with a size of 16 mm, the small side of the specimen A with a size of 30 mm and the long side of the specimen marked “B” with a size of 60 mm were measured. Figure 2a,b and Figure 3a,b show the measurement process.
Figure 2.
Specimen measured. (a) Measurement of “f”; (b) Measurement of the hexagonal SW.
Figure 3.
Specimen measured. (a) Measurement of A; (b) Measurement of the hexagonal B.
The experimental design applied aims to obtain a database with a minimum of tests without compromising outcome results. The methodology may also be used for other engineering experiments. The accuracy of the measured quantity is consistent with modern engineering requirements for accuracy and precision.
3. Results and Discussion
The experimental results obtained from the measurement of the dimensions listed in the previous point are shown in Table 2.
Table 2.
Dimensional results of the selected sizes.
We have previously performed a variance statistical analysis to determine the parameters.
The range in which the sample values vary is given by:
The standard deviation provides information about the deviation of the values in the sample from the arithmetic mean.:
The coefficient of variation expresses the dispersion in percentages:
From the obtained value of the coefficient of variation, we can say that the sample is relatively homogeneous.
The coefficient of asymmetry can be represented by the following equation [12]:
where S is the standard deviation, and is the third central moment:
The coefficient of kurtosis is determined by the equation [13]:
where is the fourth central moment.
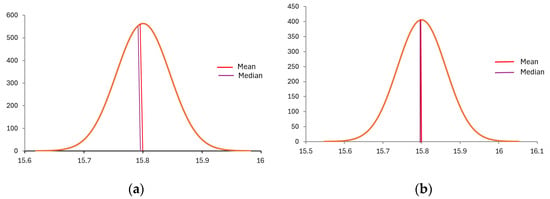
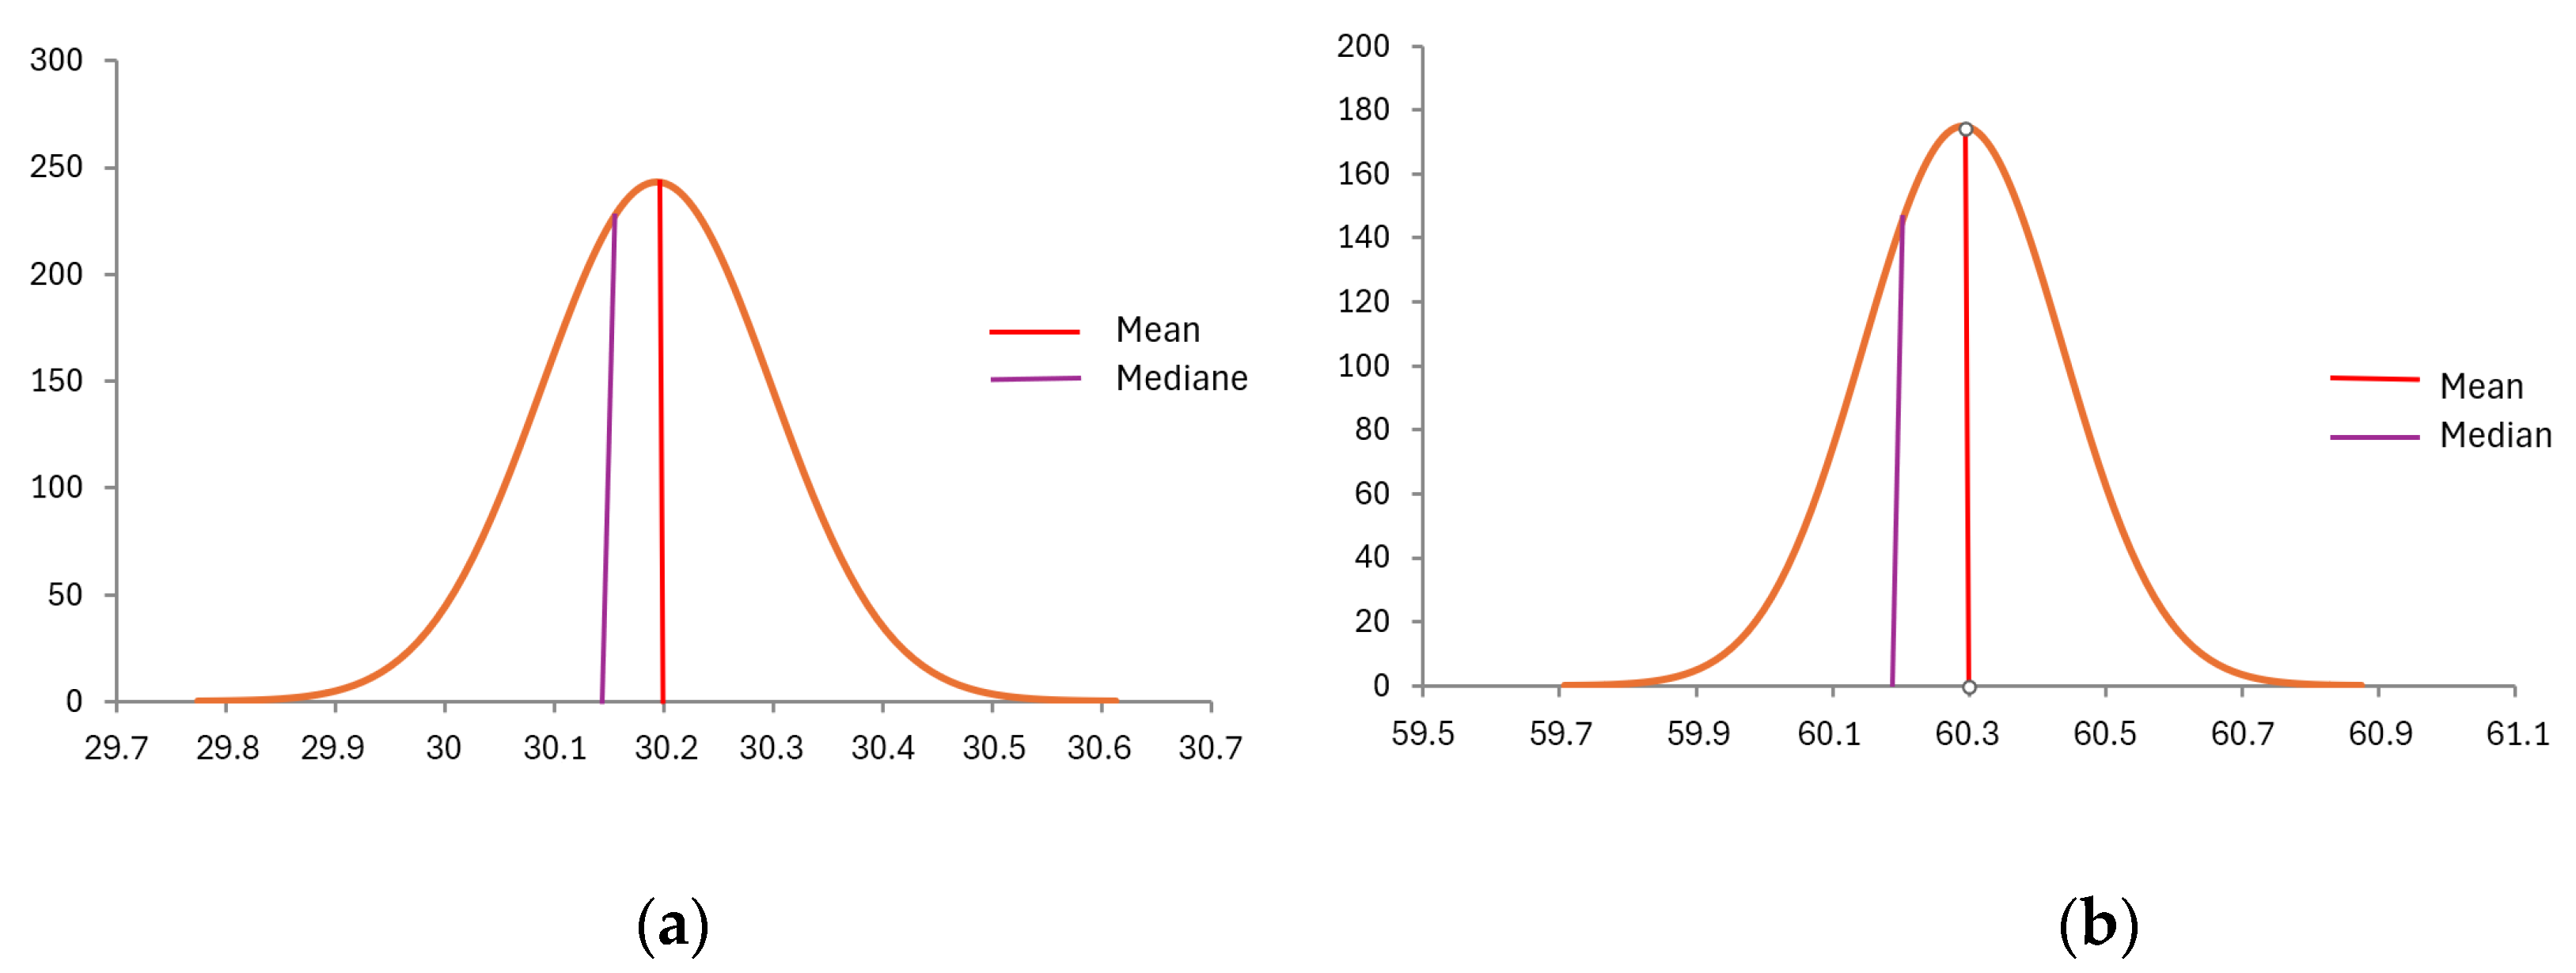
We have graphically presented a diagram of the normal distribution of the hole measurement results in Figure 4a.
Figure 4.
Results: (a) Normal distribution of measured hole data; (b) Normal distribution of measured data for the hexagon.
The summary of the statistical approach is presented in Table 3.
Table 3.
Statistical summary for Hole f [mm].
Since the coefficient of variation is V = 0.0021 ≤ 10 the sample is uniform. The distribution is symmetric about X the perpendicular, lowered to the abscissa at point, because the coefficient of asymmetry As = 0.33. The distribution has a reduced kurtosis because Ex = −1.1 < 0.
Results of the variational statistical analysis for the hexagonal hole SW 16 mm presented in Figure 4b.
In the statistical processing of the measured results of the hexagon, the coefficient of variation is V = 0.0022 ≤ 10, so the sample is uniform. The distribution is symmetrical about the perpendicular, lowered to the abscissa at point X, because the coefficient of asymmetry As = −0.6. The distribution has a reduced kurtosis because Ex = −0.91 < 0. The statistical summary is shown in Table 4.
Table 4.
Statistical summary for Hexagonal SW.
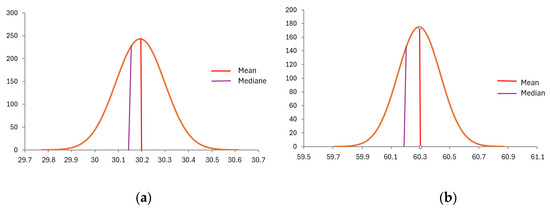
Figure 5.
Results: (a) Normal distribution of measured data for size A; (b) Normal distribution of measured data for the dimension B.
Table 5.
Statistical summary for Size А.
From the statistical analysis for the wall with size A, we obtain the coefficient of variation V = 0.0011 ≤ 10; therefore, the sample is uniform. The distribution is asymmetric with a right-extended shoulder because the coefficient of asymmetry As = 1.29 > 0. The distribution has a normal kurtosis because Ex = −0.17 ≤ 0.
Results of the statistical analysis of variation for the hexagonal side B 60 mm (Figure 5b, Table 6).
Table 6.
Statistical summary for Size B.
From the statistical analysis for the wall with size B, we obtain the coefficient of variation V = 0.0021 ≤ 10; therefore, the sample is uniform. The distribution is asymmetric with a right-skewed shoulder because the coefficient of asymmetry As = 1.39 > 0. The distribution has a normal kurtosis because Ex = −0.05 ≤ 0.
Although the above conclusions have been made, a regression single-factor statistical analysis must be performed to determine how the factors affect the dimensions accuracy.
The experimental data from Table 2 were processed mathematically and statistically with the MINITAB software product. For the mathematical description of the target function, the following linear regression model was obtained, describing four regression equations for each dimension [14]:
Table 7, Table 8, Table 9 and Table 10 present the coefficient values. T-value is used to determine whether the coefficients are significant. However, the p-value is used more often, since the threshold for rejecting the null hypothesis does not depend on the degrees of freedom. In this case, the p-value for each coefficient is lower than 0.05, so the null hypothesis is rejected. The coefficients of all 4 regression models are statistically significant. T-value and p-value are linked. A high T-value and low p-value indicate a strong effect with little variation.
Table 7.
Coefficients of function “hole”.
Table 8.
Coefficients of function “hexagon”.
Table 9.
Coefficients of dimensional function “A”.
Table 10.
Coefficients of function dimension “B”.
From Table 11, Table 12, Table 13 and Table 14 it may be concluded that the coefficient of determination is very high, which means the model fits the data and the experiment is well planned and conducted. For the four regression equations, the coefficient is over 90%. Therefore, over 90% of the values of the model factors directly affect the regression models.
Table 11.
Summary model of hole.
Table 12.
Summary model of hexagon.
Table 13.
Summary model of “A”.
Table 14.
Summary model of “B”.
From Table 15, Table 16, Table 17 and Table 18, the F-value and p-value results are similar to the previus one, and it may be concluded that the obtained math model is adequate according to the research and the experimental data. The main TBO goals of the engineering research have been fulfilled—reliable data have been obtained with a minimum of experiments.
Table 15.
Analysis of variance: hole.
Table 16.
Analysis of variance: hexagon.
Table 17.
Analysis of variance: dimension A.
Table 18.
Analysis of variance: dimension B.
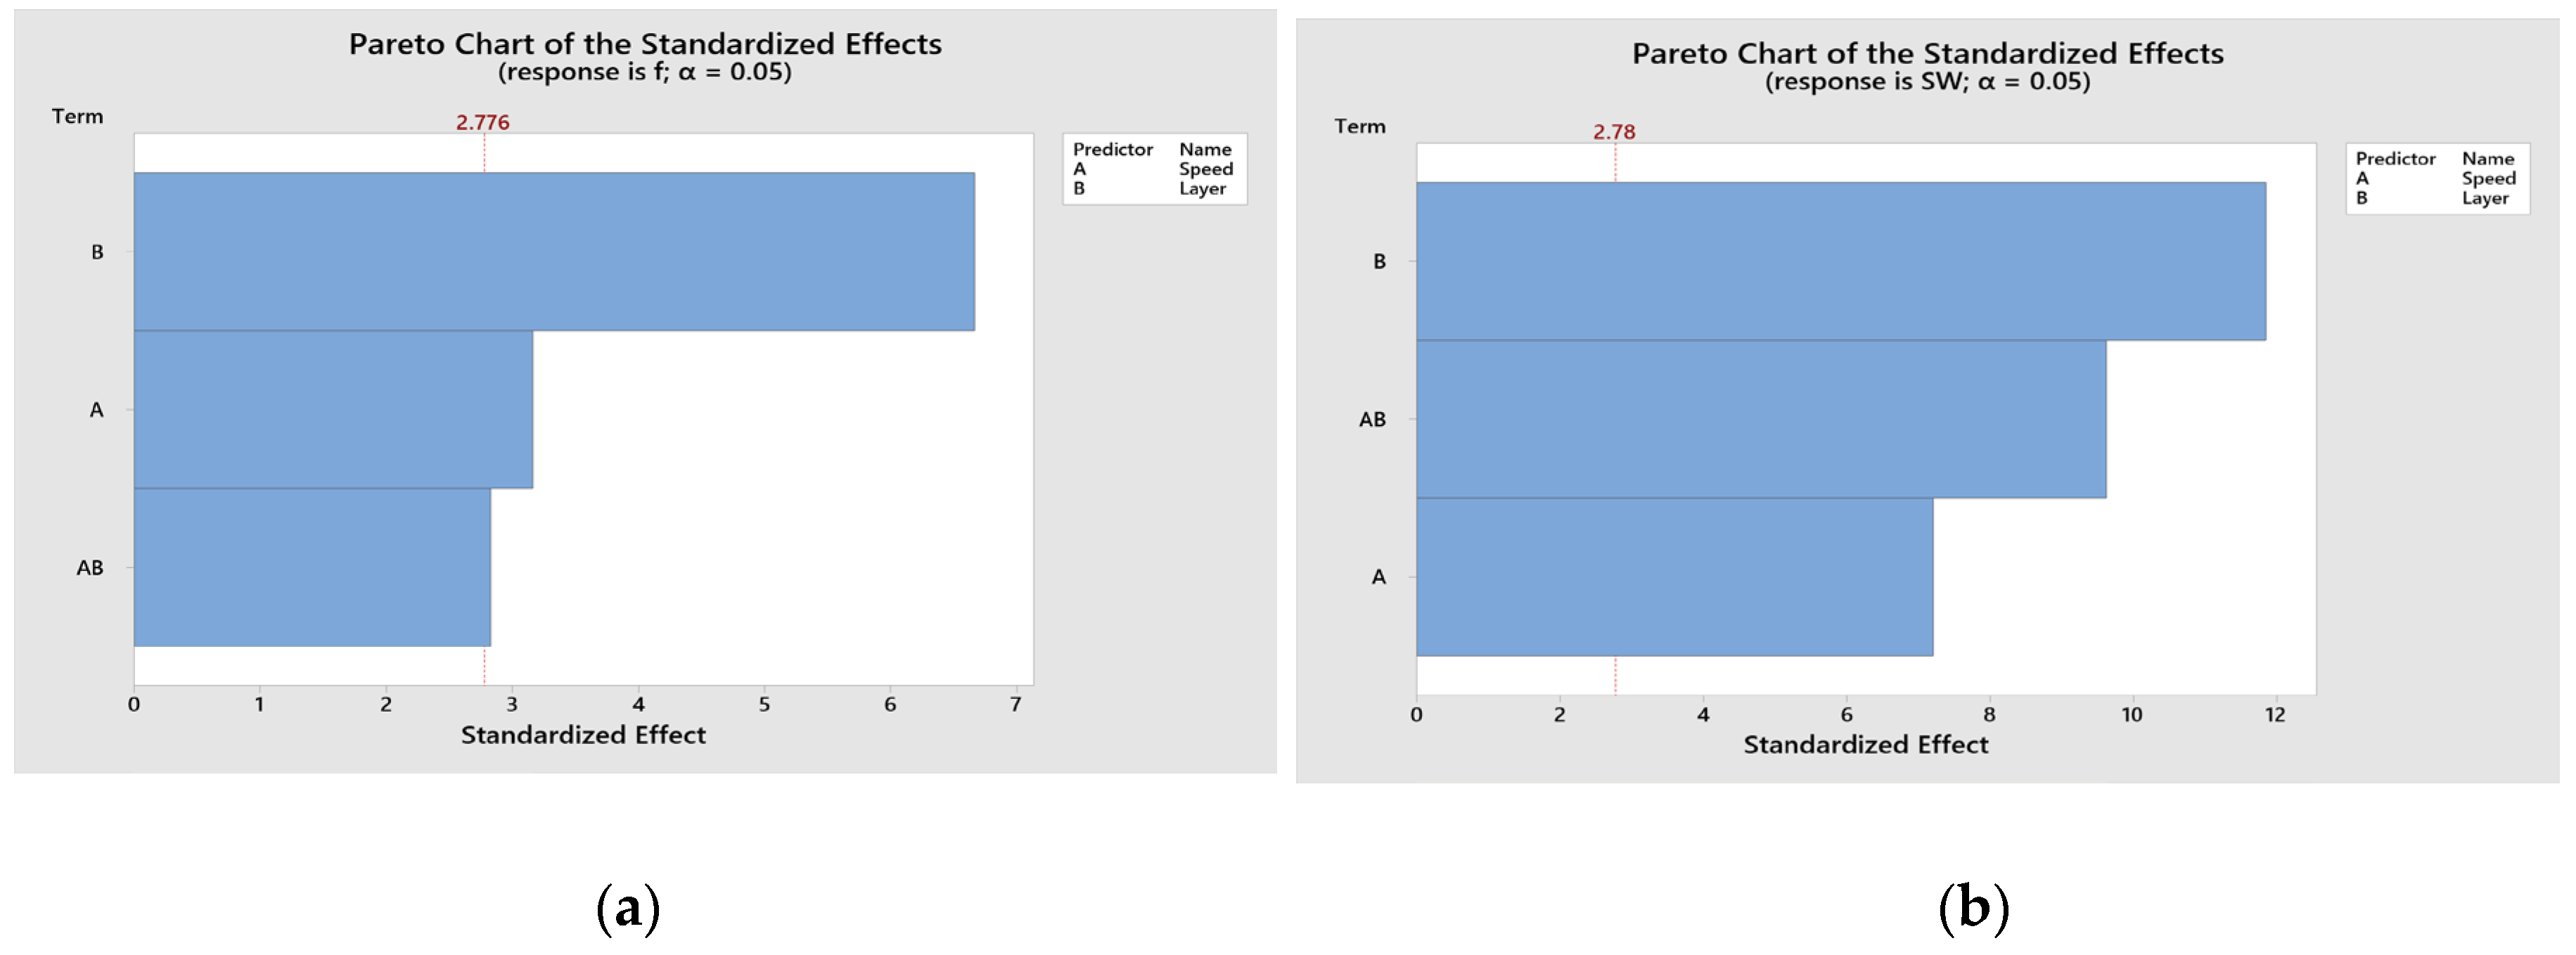
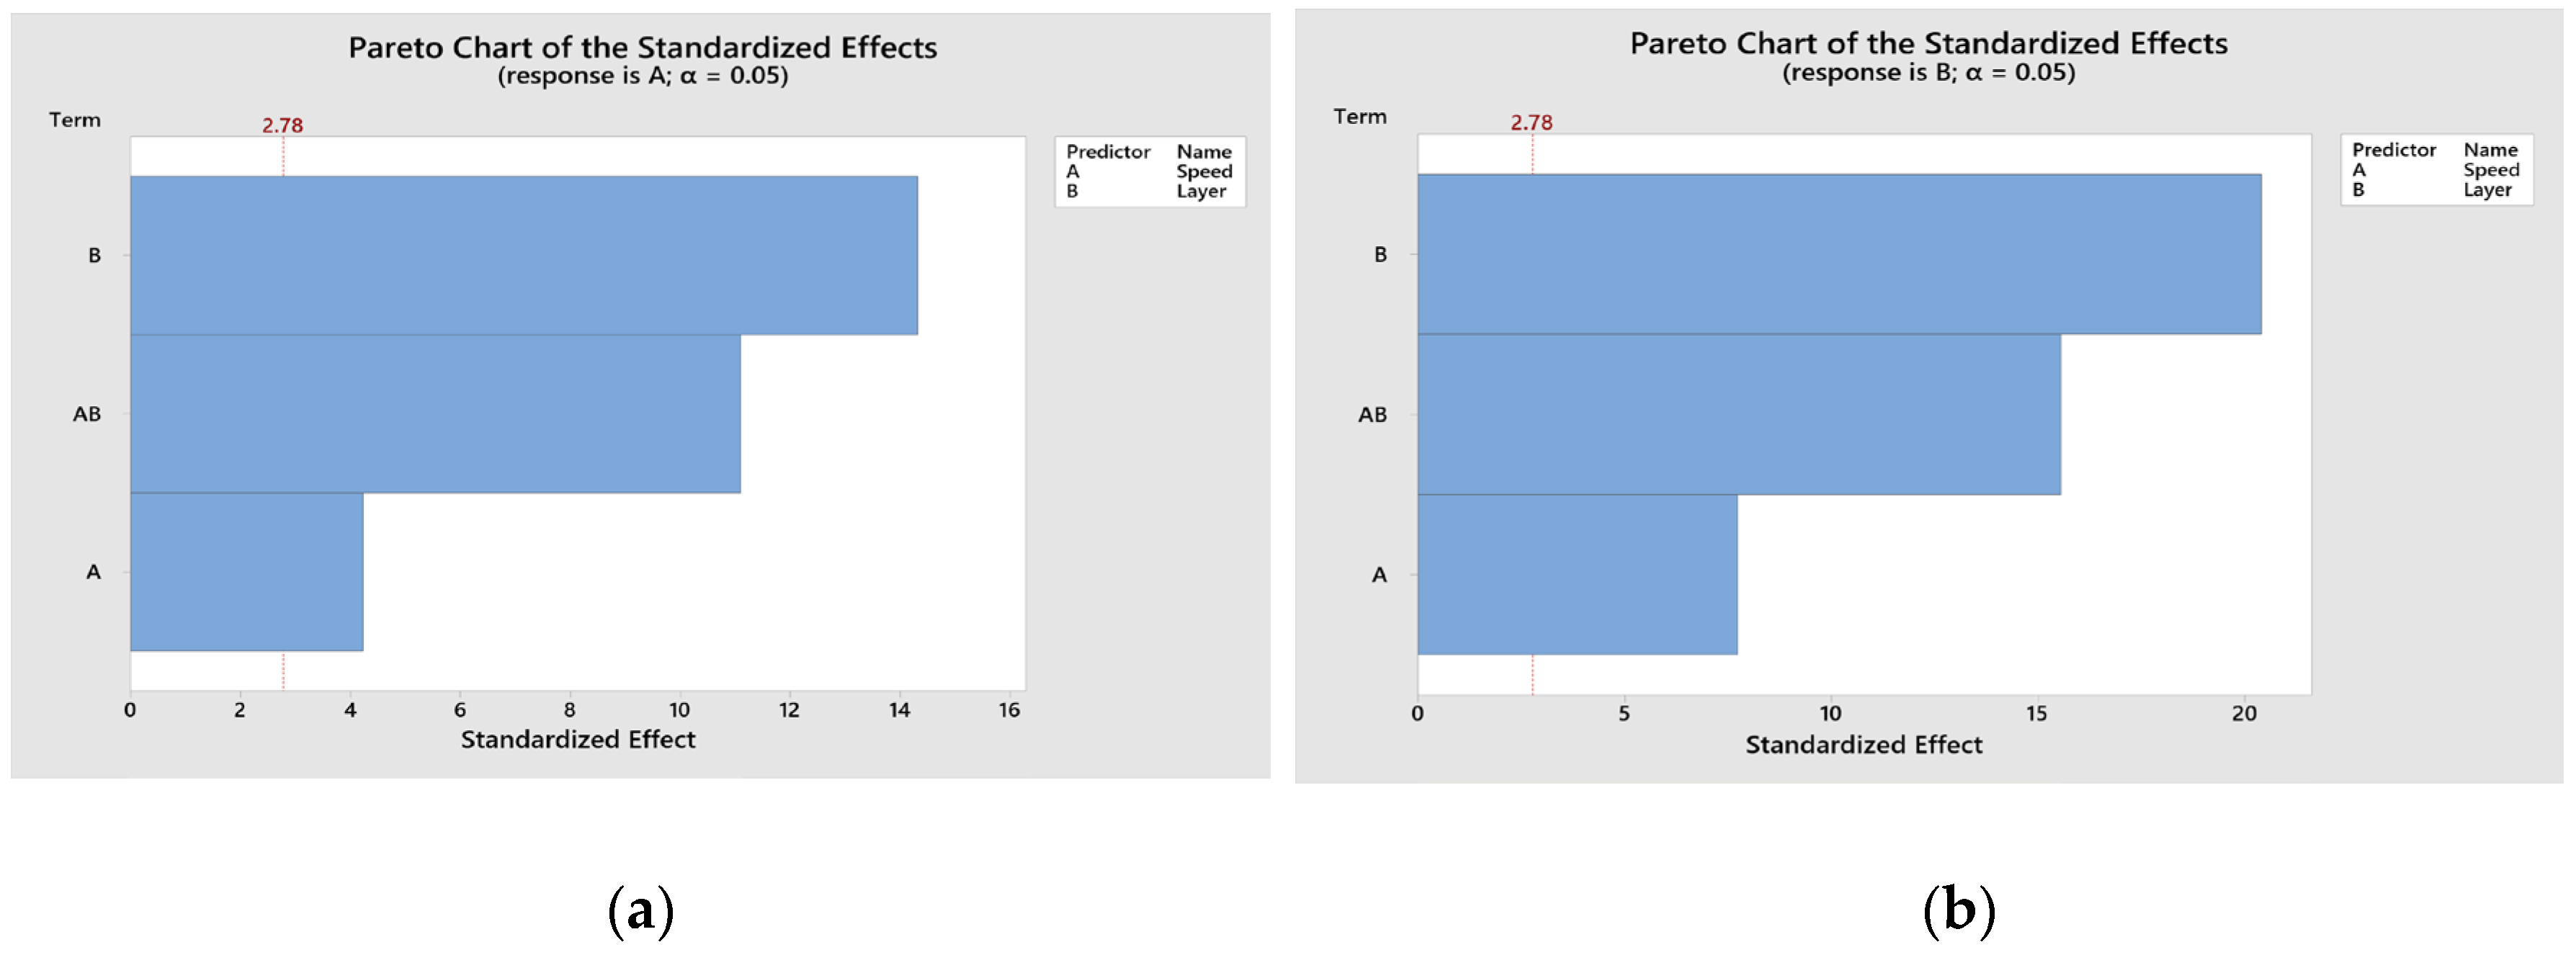
The Pareto diagram, Figure 6a,b and Figure 7a,b, arranges the coefficients according to their effect on the target function from the largest to the smallest. The diagram also draws a reference line to show where the limit of statistical significance is. It can be seen that the components pass the significance line; therefore, they are significant [15].
Figure 6.
Results: (a) Pareto diagram hole; (b) Pareto diagram hexagon.
Figure 7.
Results: (a) Pareto diagram of size A; (b) Pareto diagram of size B.
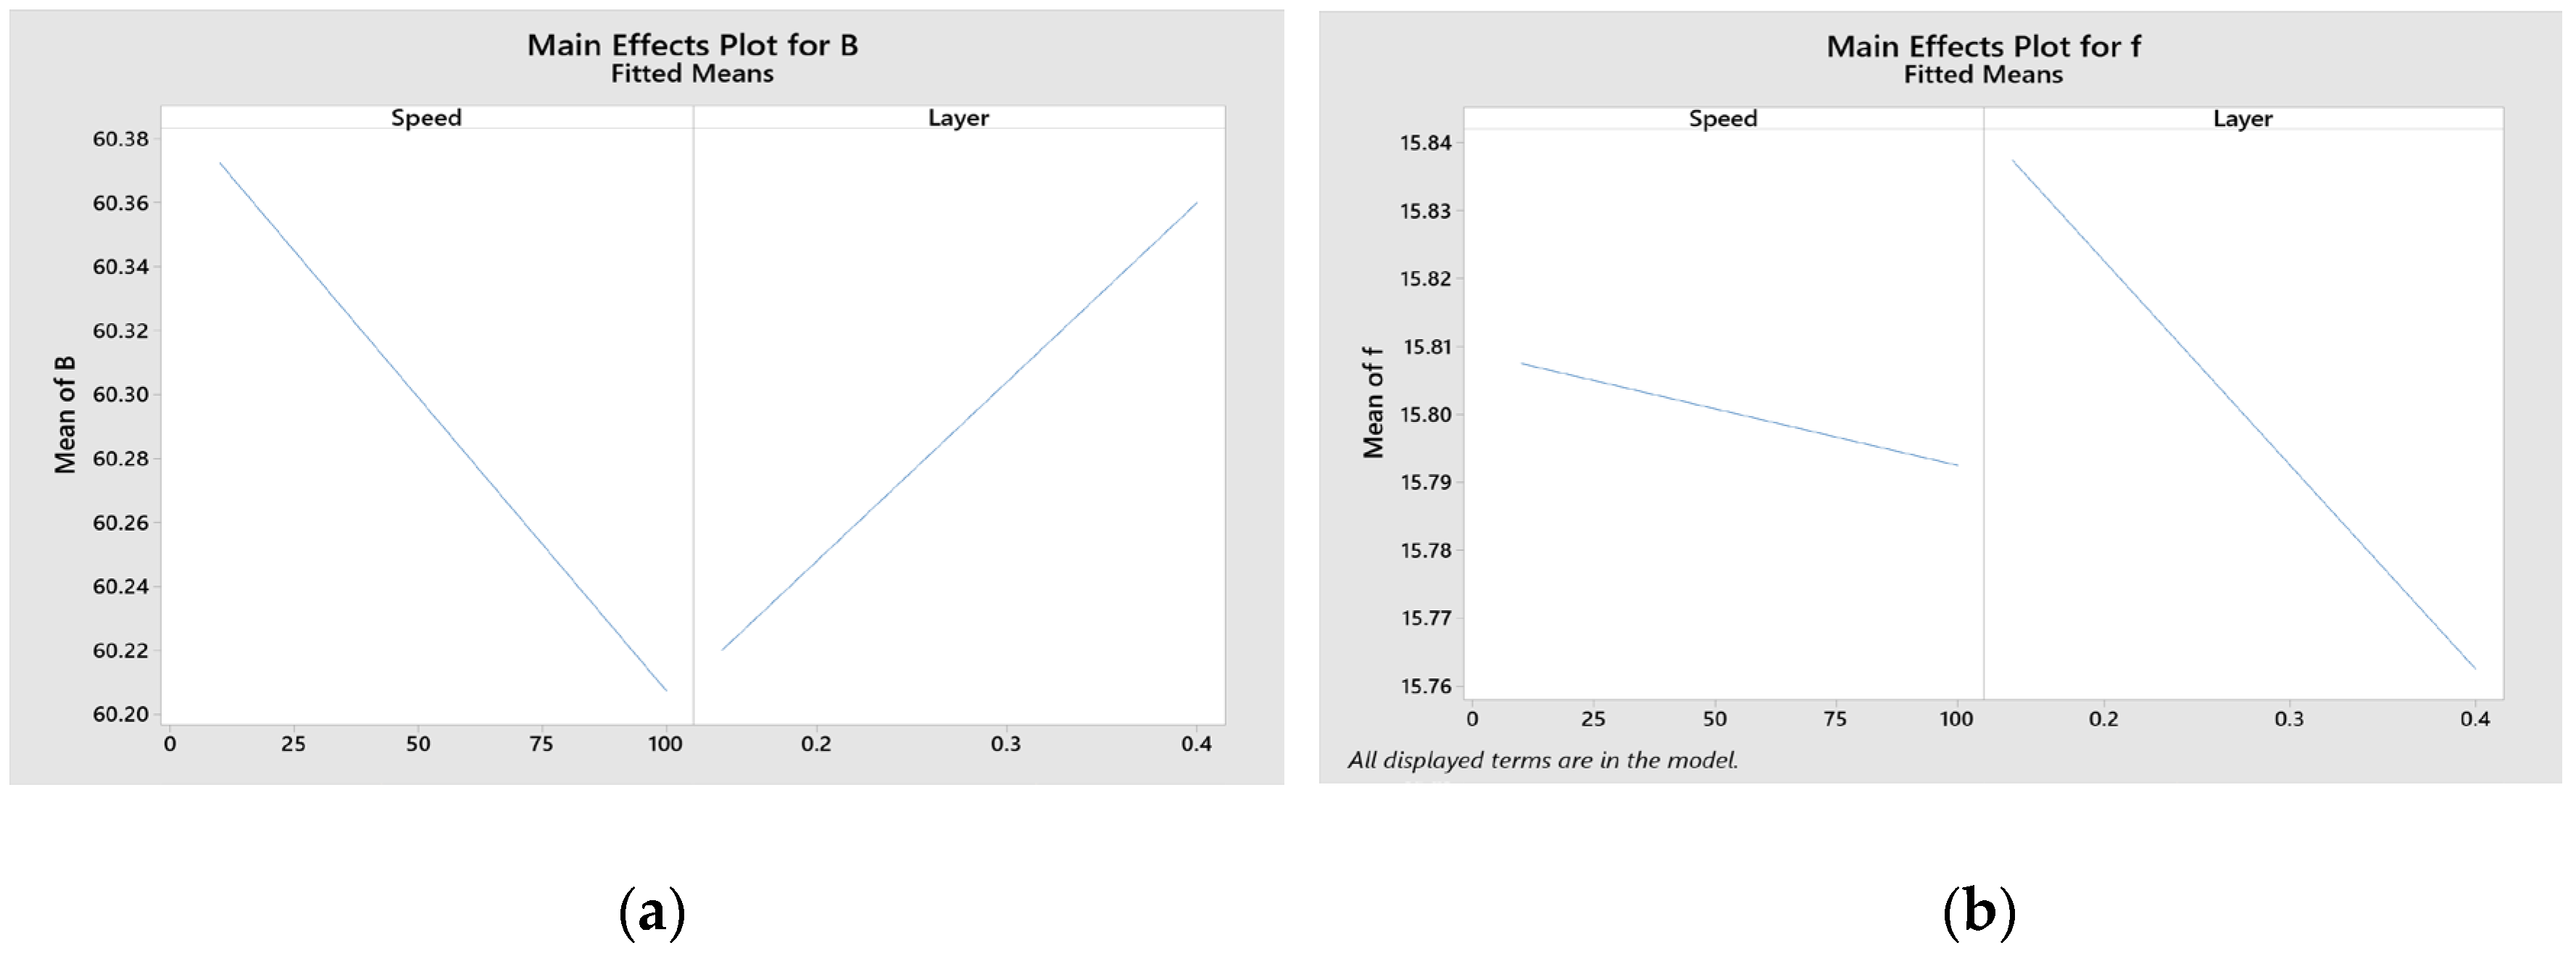
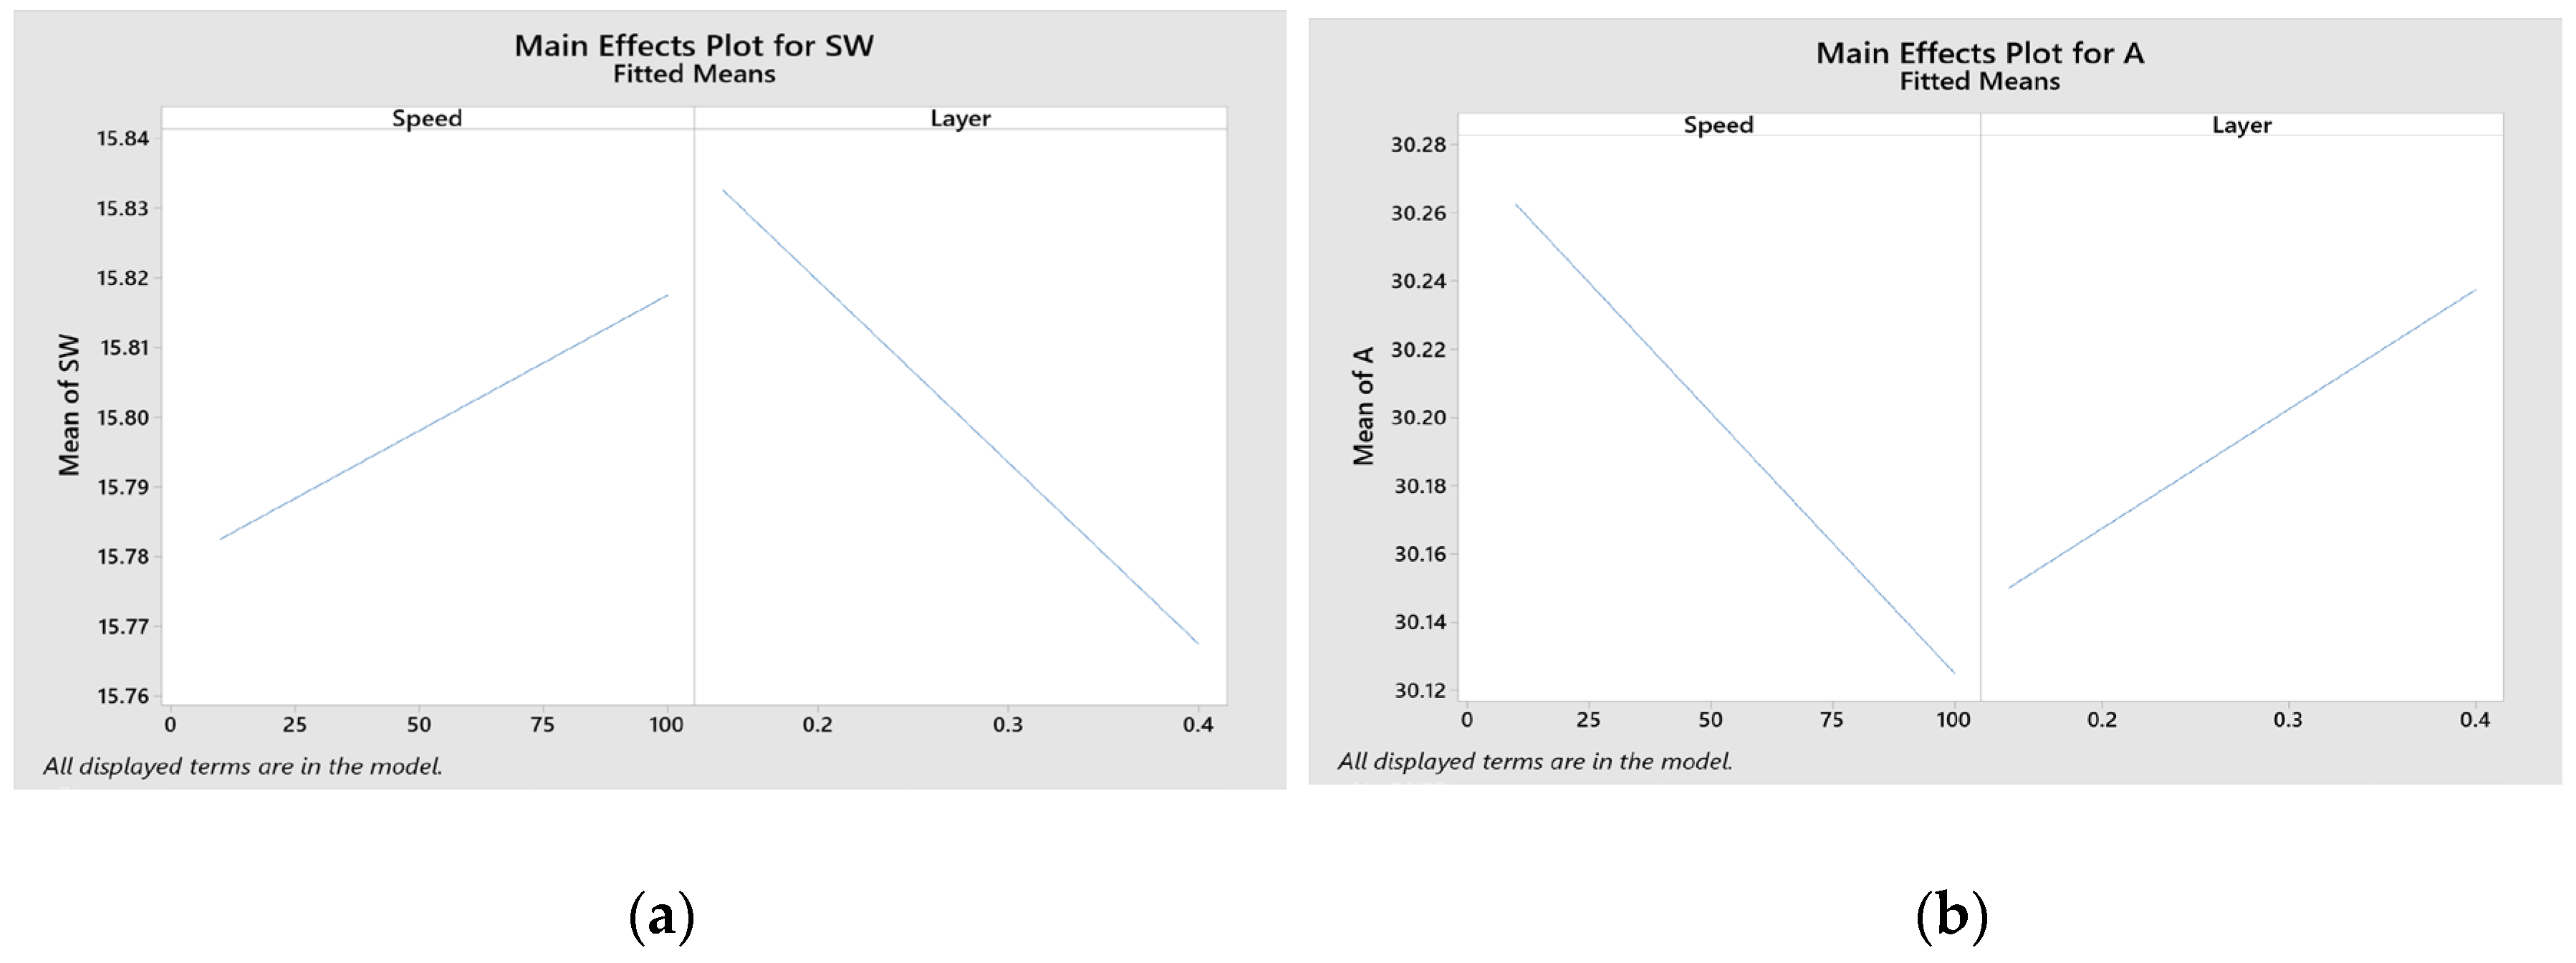
Figure 8a,b and Figure 9a,b show the graphs of the influence between each of the factors against the regression equation.
Figure 8.
Results: (a) main plot “B”; (b) main plot “f”.
Figure 9.
Results: (a) main plot “SW”; (b) main plot “A”.
We can explain the different slope in Figure 8a,b by the fact that the dimensions are rotational; when printing, the size increases towards the inside of the hole and the hexagon, that is, the size decreases. For the outer dimensions, the tension is reversed.
An optimization was performed as shown in Table 19. Based on a preliminary analysis of the experimental results, we have set a certain interval for each of the dimensions.
Table 19.
Possible solution.
From the analysis of the results and statistical work, the optimal option is a low printing speed and low filament thickness (Table 19). High filament thicknesses lead to lower density and greater deviation from dimensional accuracy [16].
The greatest influence on dimensional accuracy is the printing speed, since the printing speed affects the flow of liquid filament [17].
4. Conclusions
From the obtained results, the following conclusions are determined:
- From the study, we can conclude that the greatest influence on the accuracy of the size is the printing speed.
- The performed variation analysis shows a 95% probability that the size tolerance varies in the range from 0.13 to 0.34 mm
- From the optimization, we can say with a 95% probability that at a printing speed of 100 mm/s and 0.15 mm, the samples have the highest size accuracy.
- The accuracy of the sample dimensions is greatest at small print layer heights and low speeds.
- The resulting regression model and the subsequent optimization allow us to say with a 95% probability that at a printing speed of 100 mm/s and 0.15 mm layer height, the accuracy of the sample dimensions will be in the confidence interval for the hole from 15.79 to 15.87; for the hexagon from 15.76 to 15.94; for size A from 29.97 to 30.19; and for size B from 59.97 to 60.30 mm.
- Based on the above conclusions, we can conclude that 3D printing of PA6-CF material should be performed at the lowest possible printing speeds and the minimum possible layer height.
Author Contributions
Conceptualization, V.B., S.S. and K.C.; methodology, K.C.; software, S.S.; validation, V.B., S.S. and K.C.; formal analysis, V.B.; investigation, K.C.; resources, S.S.; data curation, K.C.; writing—original draft preparation, K.C.; writing—review and editing, V.B.; visualization, V.B.; supervision, V.B.; project administration, K.C.; funding acquisition, S.S. All authors have read and agreed to the published version of the manuscript.
Funding
This research was funded by the European Regional Development Fund within the OP “Research, Innovation and Digitalization Programme for Intelligent Transformation 2021–2027”, Project № BG16RFPR002-1.014-0005 Center of Competence “Smart Mechatronics, Eco- and Energy Saving Systems and Technologies”.
Institutional Review Board Statement
Not applicable.
Informed Consent Statement
Not applicable.
Data Availability Statement
Data will be available on request.
Conflicts of Interest
The authors declare no conflicts of interest.
Abbreviations
The following abbreviations are used in this manuscript:
| PLA | Polylactic acid |
| ABS | Acrylonitrile butadiene styrene |
| PETG | Polyethylene terephthalate |
| PEEK | Polyether ether ketone |
| PEI | Polyethylenimine |
References
- Cheng, J.; Tan, E.; Kang, L. Pharmacy 3D Printing. Biofabrication 2024, 17, 012002. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Xu, Y. Types and Applications of 3D Printing. Highlights Sci. Eng. Technol. 2024, 119, 697–702. [Google Scholar] [CrossRef] [Scilit]
- Serrano, D.R.; Kara, A.; Yuste, I.; Luciano, F.C.; Ongoren, B.; Anaya, B.J.; Molina, G.; Diez, L.; Ramirez, B.I.; Ramirez, I.O.; et al. 3D Printing Technologies in Personalized Medicine, Nanomedicines, and Biopharmaceuticals. Pharmaceutics 2023, 15, 313. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Mahajan, H.; Gule, O.; Malpure, A. Design and Optimization of 3D Printing Process Parameters. Available online: https://www.researchgate.net/publication/382560722_DESIGN_AND_OPTIMIZATION_OF_3D_PRINTING_PROCESS_PARAMETERS (accessed on 30 May 2025).
- Petrov, M.A.; Hung, T.D. Application of 3D-Printing Technologies in Manufacturing of Tools for Microforming of Sheet Metal Blanks; Omsk State Technical University: Omsk, Russia, 2024; pp. 411–417. [Google Scholar] [CrossRef] [Scilit]
- Rahman, M.A.; Gibbon, L.; Islam, M.Z.; Hall, E.; Ulven, C. Adjustment of Mechanical Properties of 3D Printed Continuous Carbon Fiber-Reinforced Thermoset Composites by Print Parameter Adjustments. Polymers 2024, 16, 2996. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Alghauli, M.; Almuzaini, S.; Aljohani, R.; Alqutaibi, A. Influence of 3D Printing Orientations on Physico-Mechanical Properties and Accuracy of Additively Manufactured Dental Ceramics. J. Prosthodont. 2025, 69, 181–202. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Murariu, A.C.; Sirbu, A.; Cocard, M.; Duma, I. Influence of 3D Printing Parameters on Mechanical Properties of the PLA Parts Made by FDM Additive Manufacturing Process. Eng. Innov. 2022, 2, 7–20. [Google Scholar] [CrossRef] [Scilit]
- Eteje, S.O.; Ifuwe, C.; Oduyebo, O. Precision and Accuracy Determination of Horizontal Geodetic Networks Using Least Squares Technique. Caliph. J. Sci. Technol. 2024, 6, 265–272. [Google Scholar] [CrossRef] [Scilit]
- Liacouras, P.; Huo, E.; Mitsouras, D. 3D Printing Technologies and Materials; Springer: Cham, Switzerland, 2024. [Google Scholar] [CrossRef] [Scilit]
- Liu, J.; He, L.; Yang, D.; Liang, J.; Zhao, R.; Wang, Z.; Li, X.; Chen, Z. Effects of Carbon Fiber Content on the Crystallization and Rheological Properties of Carbon Fiber-Reinforced Polyamide. Polymers 2024, 16, 2395. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Hisam, M.; Dar, A.; Elrasheed, M.; Khan, M.; Gera, R.; Azad, I. The Versatility of the Taguchi Method: Optimizing Experiments Across Diverse Disciplines. J. Stat. Theory Appl. 2024, 23, 365–389. [Google Scholar] [CrossRef] [Scilit]
- Rodríguez, A.A.; Reyes, C.; Vita, A.; Quintana, R.; Golubev, D.; Agusti, D.; Abal, A.; Portaz, E. Prediction of Injuries in Elite Soccer Players with the Analysis of Asymmetries in the CMJ Through the Use of Machine Learning Tools. Preprints 2025, 2025041448. [Google Scholar] [CrossRef] [Scilit]
- Merabet, L.; Boucerredj, L.; Behim, M.; Khechekhouch, A. Comparative Study of Kurtosis and L-Kurtosis for Bearing Fault Classification in Induction Motors. Stud. Eng. Exact Sci. 2024, 5, e12489. [Google Scholar] [CrossRef] [Scilit]
- Geng, Y.; Li, Q.; Yang, G.; Qiu, W. Linear Regression. In Practical Machine Learning Illustrated with KNIME; Springer: Singapore, 2024. [Google Scholar] [CrossRef] [Scilit]
- Funke, D.; Hespe, D.; Sanders, P.; Storandt, S.; Truschel, C. Pareto Sums of Pareto Sets: Lower Bounds and Algorithms. arXiv 2024. [Google Scholar] [CrossRef] [Scilit] [PubMed]
- Agarwal, K.M.; Shubham, P.; Bhatia, D.; Sharma, P.; Vaid, H.; Vajpeyi, R. Analyzing the Impact of Print Parameters on Dimensional Variation of ABS Specimens Printed Using Fused Deposition Modelling (FDM). Sens. Int. 2022, 3, 100149. [Google Scholar] [CrossRef] [Scilit]

Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2025 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license (https://creativecommons.org/licenses/by/4.0/).