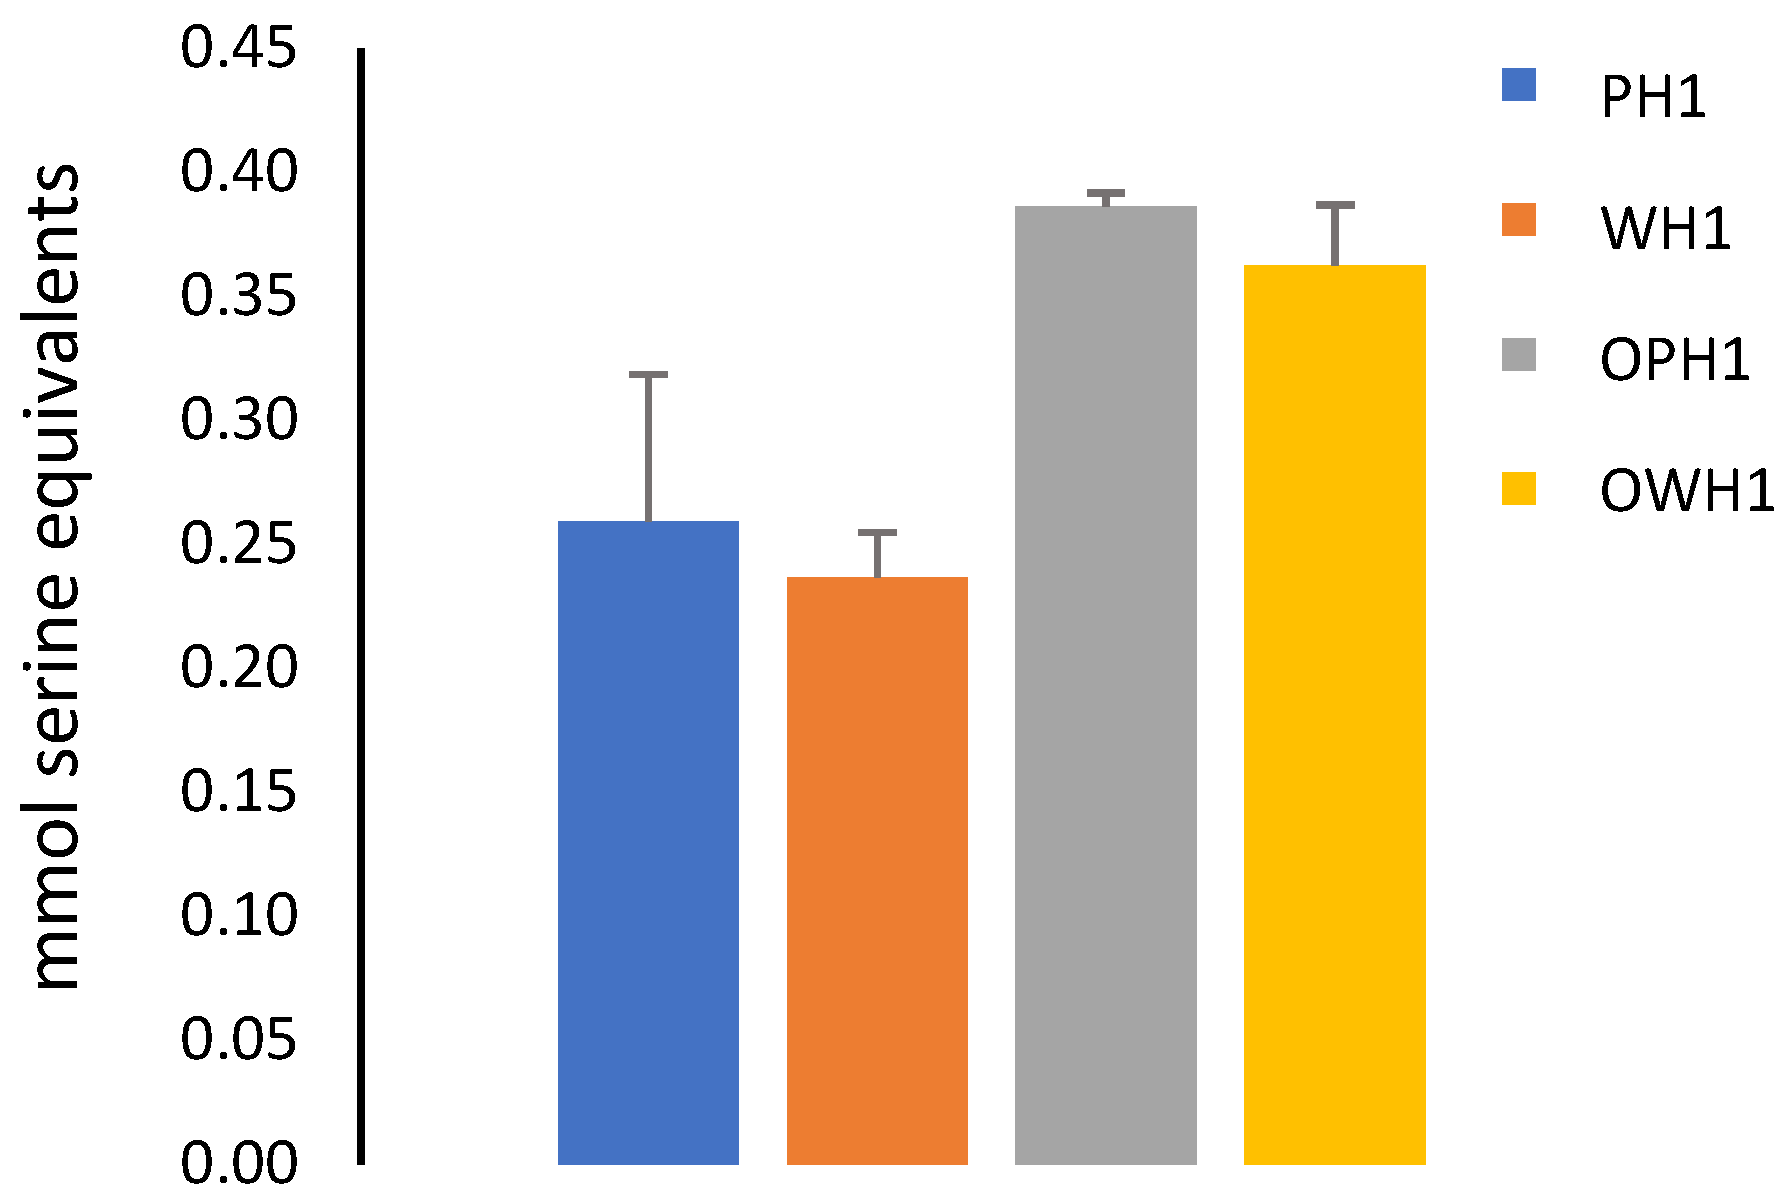1. Introduction
The increasing global demand for sustainable food sources and ingredients for specialized diets positions sorghum (Sorghum bicolor (L.) Moench) as a crucial and rapidly evolving agricultural commodity. Sorghum is widely recognized for its robust nature, remarkable drought tolerance, and resistance to waterlogging, becoming a major staple crop, particularly across arid and semiarid regions. Sorghum is rich in nutrients, fiber, and bioactive components and is also a gluten-free alternative for individuals suffering from celiac disease or gluten intolerance, leading to its increasing incorporation into commercial products like breads, pastas, and snack foods.
Despite these significant advantages, the full potential of sorghum use is often limited by inherent drawbacks: the presence of antinutritional factors, mainly present in grain external layers, and generally poor protein and starch digestibility. To overcome these limitations, processing and modification strategies are essential to enhance both the nutritional quality and functional characteristics of sorghum flour. Typically, the primary approach involves removing or minimizing the outer layers through grain polishing before milling, allowing for the production of either whole or refined flour [
1,
2]. Traditional methods used to change flour properties, such as chemical treatments or wet cooking, often involve multiple lengthy processing stages, extensive washing, and high energy costs, which can result in the production of contaminant residues that severely limit industrial scalability.
In contrast, extrusion cooking technology offers a highly efficient, continuous, and versatile modification platform. As a high-temperature, short-time (HTST) process, extrusion is noted for its cost-effectiveness, high productivity, energy efficiency, and low waste generation. Extrusion uniquely integrates several unit operations—including mixing, conveying, kneading, cooking, shaping, and pasteurization—into a single system. The intense thermo–mechanical energy applied during extrusion (high pressure, temperature, and mechanical shear) induces profound physicochemical transformations in flours: starch gelatinization and partial degradation (dextrinization), protein denaturation, and the reduction or elimination of antinutritional factors, such as tannins, phytate, and trypsin inhibitors. To further enhance modification efficacy and address the limitations of conventional chemical treatments, the field has transitioned toward reactive extrusion. Reactive extrusion involves performing chemical or structural modifications simultaneously with the thermal and mechanical forces inside the extruder barrel, often in a single step. This advanced technique combines the process advantages of extrusion with the desired outcomes of chemical modification, minimizing chemical waste and facilitating the production of specialized ingredients [
3,
4,
5].
A promising strategy for functional modification that adheres to user and consumer-friendly demands is the use of ozone. Ozone is generally recognized as safe (GRAS) by the FDA and functions as a powerful oxidant. A key benefit of ozone over traditional chemical agents (e.g., chlorine and hydrogen peroxide) is its rapid decomposition into oxygen, which ensures no harmful chemical residues remain in the food product or the environment. The ozonation of starch leads to significant molecular and functional changes. The oxidation process primarily consists of two reactions: Initially, the substitution of hydroxyl groups in starch molecules with carbonyl and carboxyl groups, which increases the degree of substitution. This step often preferentially occurs in the amorphous region. Subsequently, especially under strong oxidation, glycosidic bonds are broken, leading to the depolymerization of starch molecules [
6,
7]. Ozone treatment alters protein structure and molecular interactions. Mild treatments promote the oxidation of sulfhydryl groups, leading to the widening of the protein, decreasing surface hydrophobicity, changing both secondary and tertiary structures, and improving in vitro protein digestibility [
8,
9,
10].
Extensive research has detailed the individual effects of modification via extrusion on sorghum flour and the properties of ozone-oxidized starches from various sources (e.g., corn, sago, tapioca, rice and cassava) [
1,
2,
4,
6]. Despite the development of reactive extrusion using other modifying agents (such as alkaline hydrogen peroxide), a significant research gap exists concerning the integration of ozone within the extrusion process (reactive extrusion) for modifying sorghum flour [
3,
5]. The current literature lacks comprehensive data on how this combined, clean-label process simultaneously influences the textural qualities, thermal characteristics, and crucial in vitro digestibility profiles of both starch and proteins in sorghum.
This study aims to establish reactive extrusion with ozone as an innovative method to improve the functional and nutritional properties of modified sorghum flour and extrudates. It specifically examines how this combined process changes the texture, thermal behavior, and in vitro digestibility of starch and proteins in sorghum flour.
2. Materials and Methods
2.1. Materials
Brown sorghum grains were supplied by Molino Carlos Boero Romano S.A.I.C. (San Francisco, Cordoba, Argentina) and cleaned following the procedure described by Curti et al. [
11]. Briefly, grains were sieved, rinsed, and dried in an air-forced oven for 24 h at 40 °C to eliminate contaminants originating from the harvest site.
To prepare polished flour, the dried sorghum grains were treated in an abrasive dehuller (PAZ-1-DTA, Zaccaria, Brazil). In this device, batches of 100 g of grains were processed and maintained inside for 120 s. Whole and polished sorghum grains were ground using a hammer mill equipped with a 1 mm screen (Pulverisette® 16, Fritsch, Germany). Whole sorghum flour (W) and polished sorghum flour (P) were kept in hermetic black plastic containers until usage.
2.2. Raw Material Composition
A proximate analysis of both sorghum flours was performed according to the standard methods of AOAC [
12] (moisture: method 925.10; ash: method 923.03; lipid: method 920.39 and protein: method 920.87). Total polyphenol content was evaluated through the Folin–Ciocalteu method according to previous sorghum product assays [
13]. Total polyphenol content (TPC) was expressed as g gallic acid (GA) per 100 g of extrudate on a dry basis.
2.3. Extrusion Cooking Process
A co-rotating twin-screw self-cleaning extruder (Process 11-Hygienic, Thermo Scientific, Berlin, Germany) equipped with eight independently controlled temperature zones was used. The extruder had a length-to-diameter (L/D) ratio of 40:1, and the die diameter was 3 mm. The arrangement of screw elements was the standard three-stage configuration, which included two kneading blocks (recommended settings for cereal flour processing). Flour was dispensed with a screw feeder at a flow rate of 2.05 kg/h. The recorded process variables were average torque, die temperature, and pressure.
Three factors were analyzed at two levels: temperature profile (
Table 1), water flow rate, and the use of either ozonated or non-ozonated water. Water flow rates were adjusted to 20 and 23% of moisture in the feeding material and were identified as low (L) and high (H), respectively. To perform the reactive extrusion, ozone was generated from industrial oxygen (95% purity) using an ozone generator unit (custom-designed model, Ozonizer). Ozone was bubbled into distilled water for 10 min at a rate of 36 mg/min and a flow of 1 L/min to achieve the maximum ozone concentration in water (1.5 mg/L). The ozonated water was stored in a bottle with a two-way cap (one connection to a filter and the other to the outlet hose) during the experimental runs.
Extrudates resulting from the extrusion cooking process were dried at 45 °C in a forced air dryer for 24 h. A fraction of dried extrudates was milled using a hammer mill (Pulverisette® 16, Fritsch, Germany) equipped with a 0.75 mm mesh and stored in sealed bags at room temperature until evaluation.
2.4. Extrudate Dimensional Characterization
The extrudate dimensional characterization was determined following the method proposed by Liu [
15], with slight modifications. The length and diameter of the extrudates were measured using a caliper. Three extrudates were randomly selected per sample. Length measurements were taken for all three, and diameter measurements were performed at four randomly chosen locations along each extrudate.
The expansion index (EI) was obtained as the ratio between the mean diameter of the extrudate and the die diameter (3 mm). Subsequently, the mass of the extrudates was determined, and the density was calculated as the ratio of mass to volume, expressed in g/cm3.
2.5. Texture of Extrudate
The fracture force, defined as the maximum force needed to break an extrudate, was measured using a three-point bending test. Ten extrudates from each sample were analyzed using a texture analyzer (Universal Testing Machine model 3342, Instron, Norwood, MA, USA) equipped with a load cell of 500 N and test speed of 50 mm min−1. Each piece of 5 cm was perpendicular, placed over the anvils, and symmetrically distributed. At least four replicates were performed for each sample. Bluehill 2® software (Version 2.27) for Windows (Instron, USA) was used for instrument operation and data collection.
2.6. Analysis of Flour Properties
2.6.1. X-Ray Photoelectron Scattering (XPS)
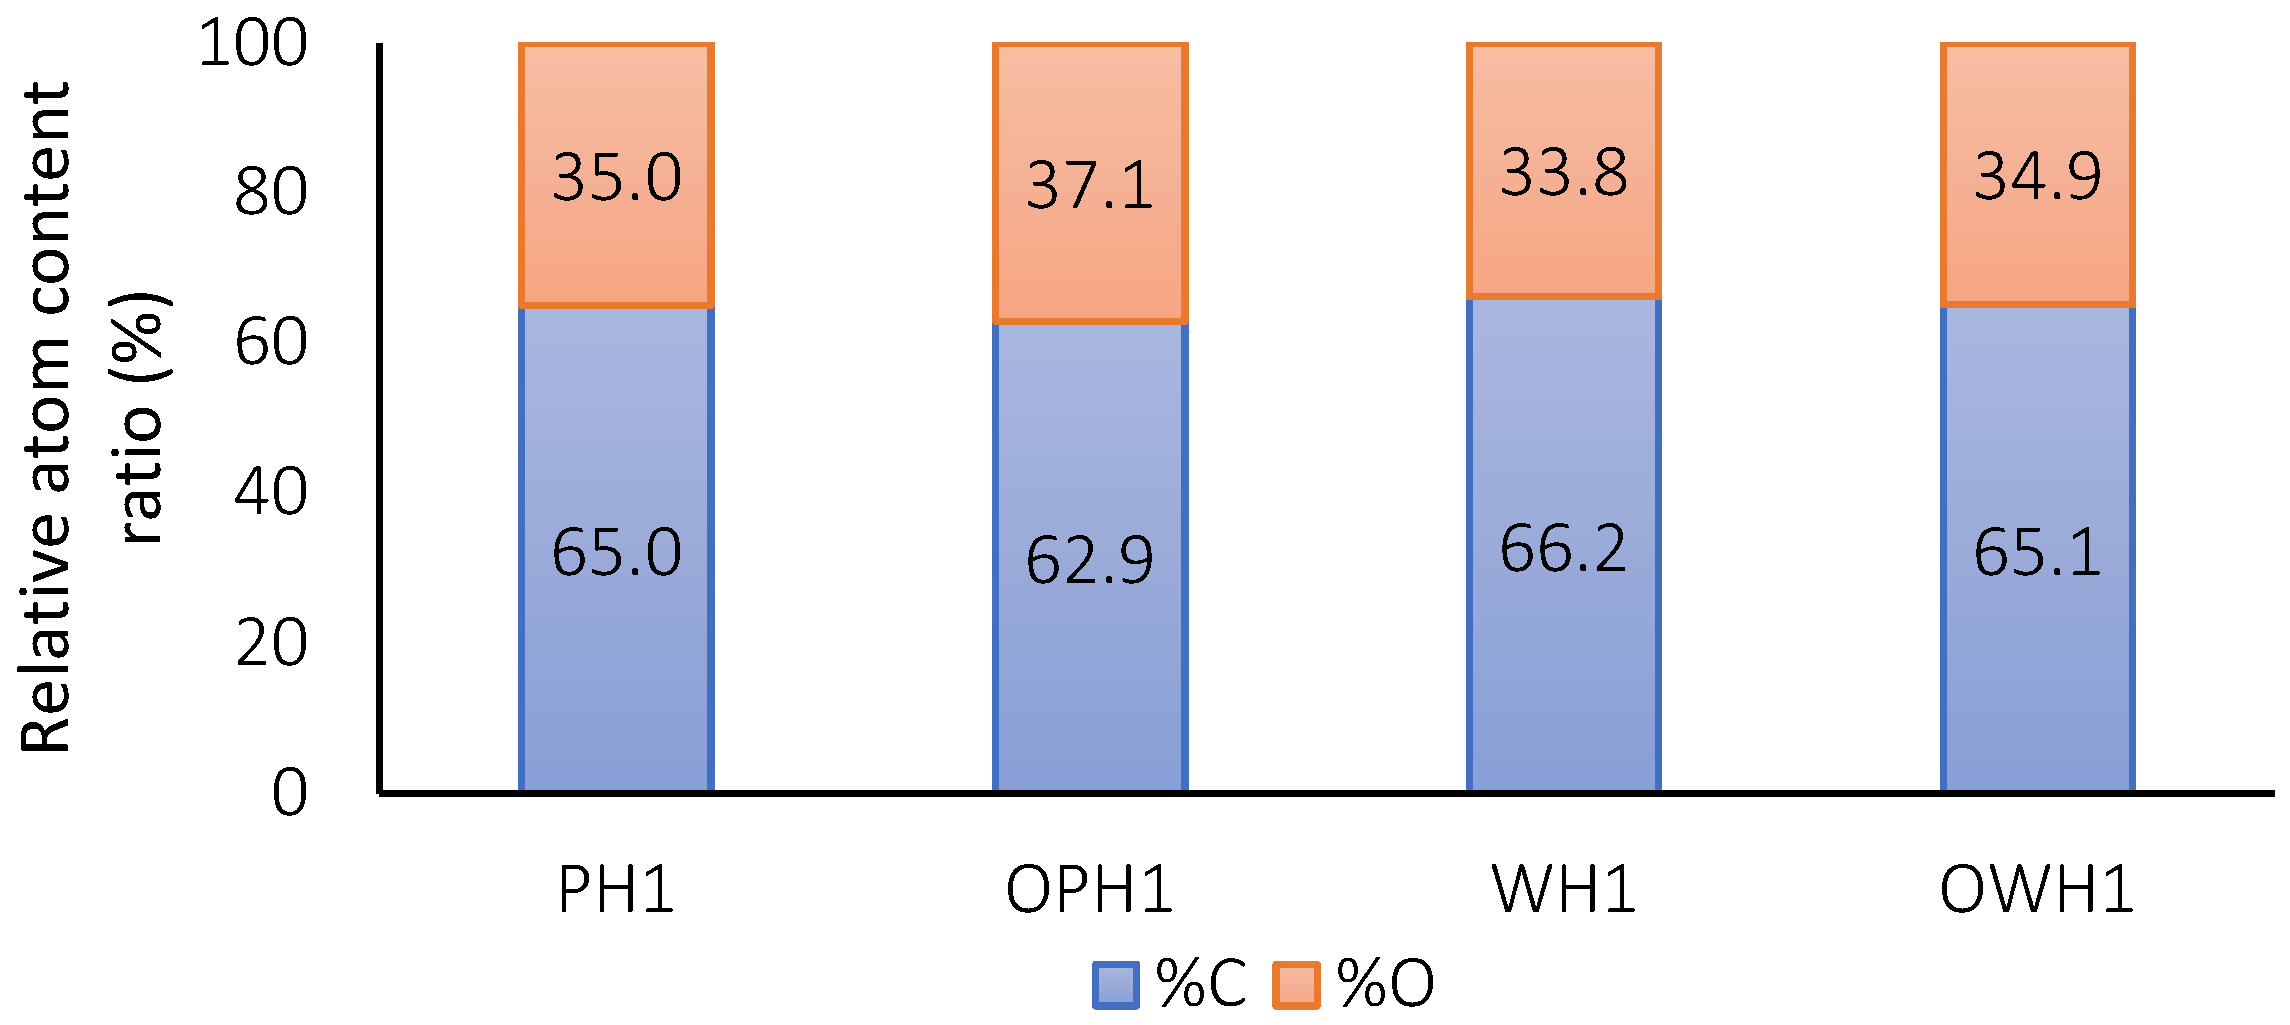
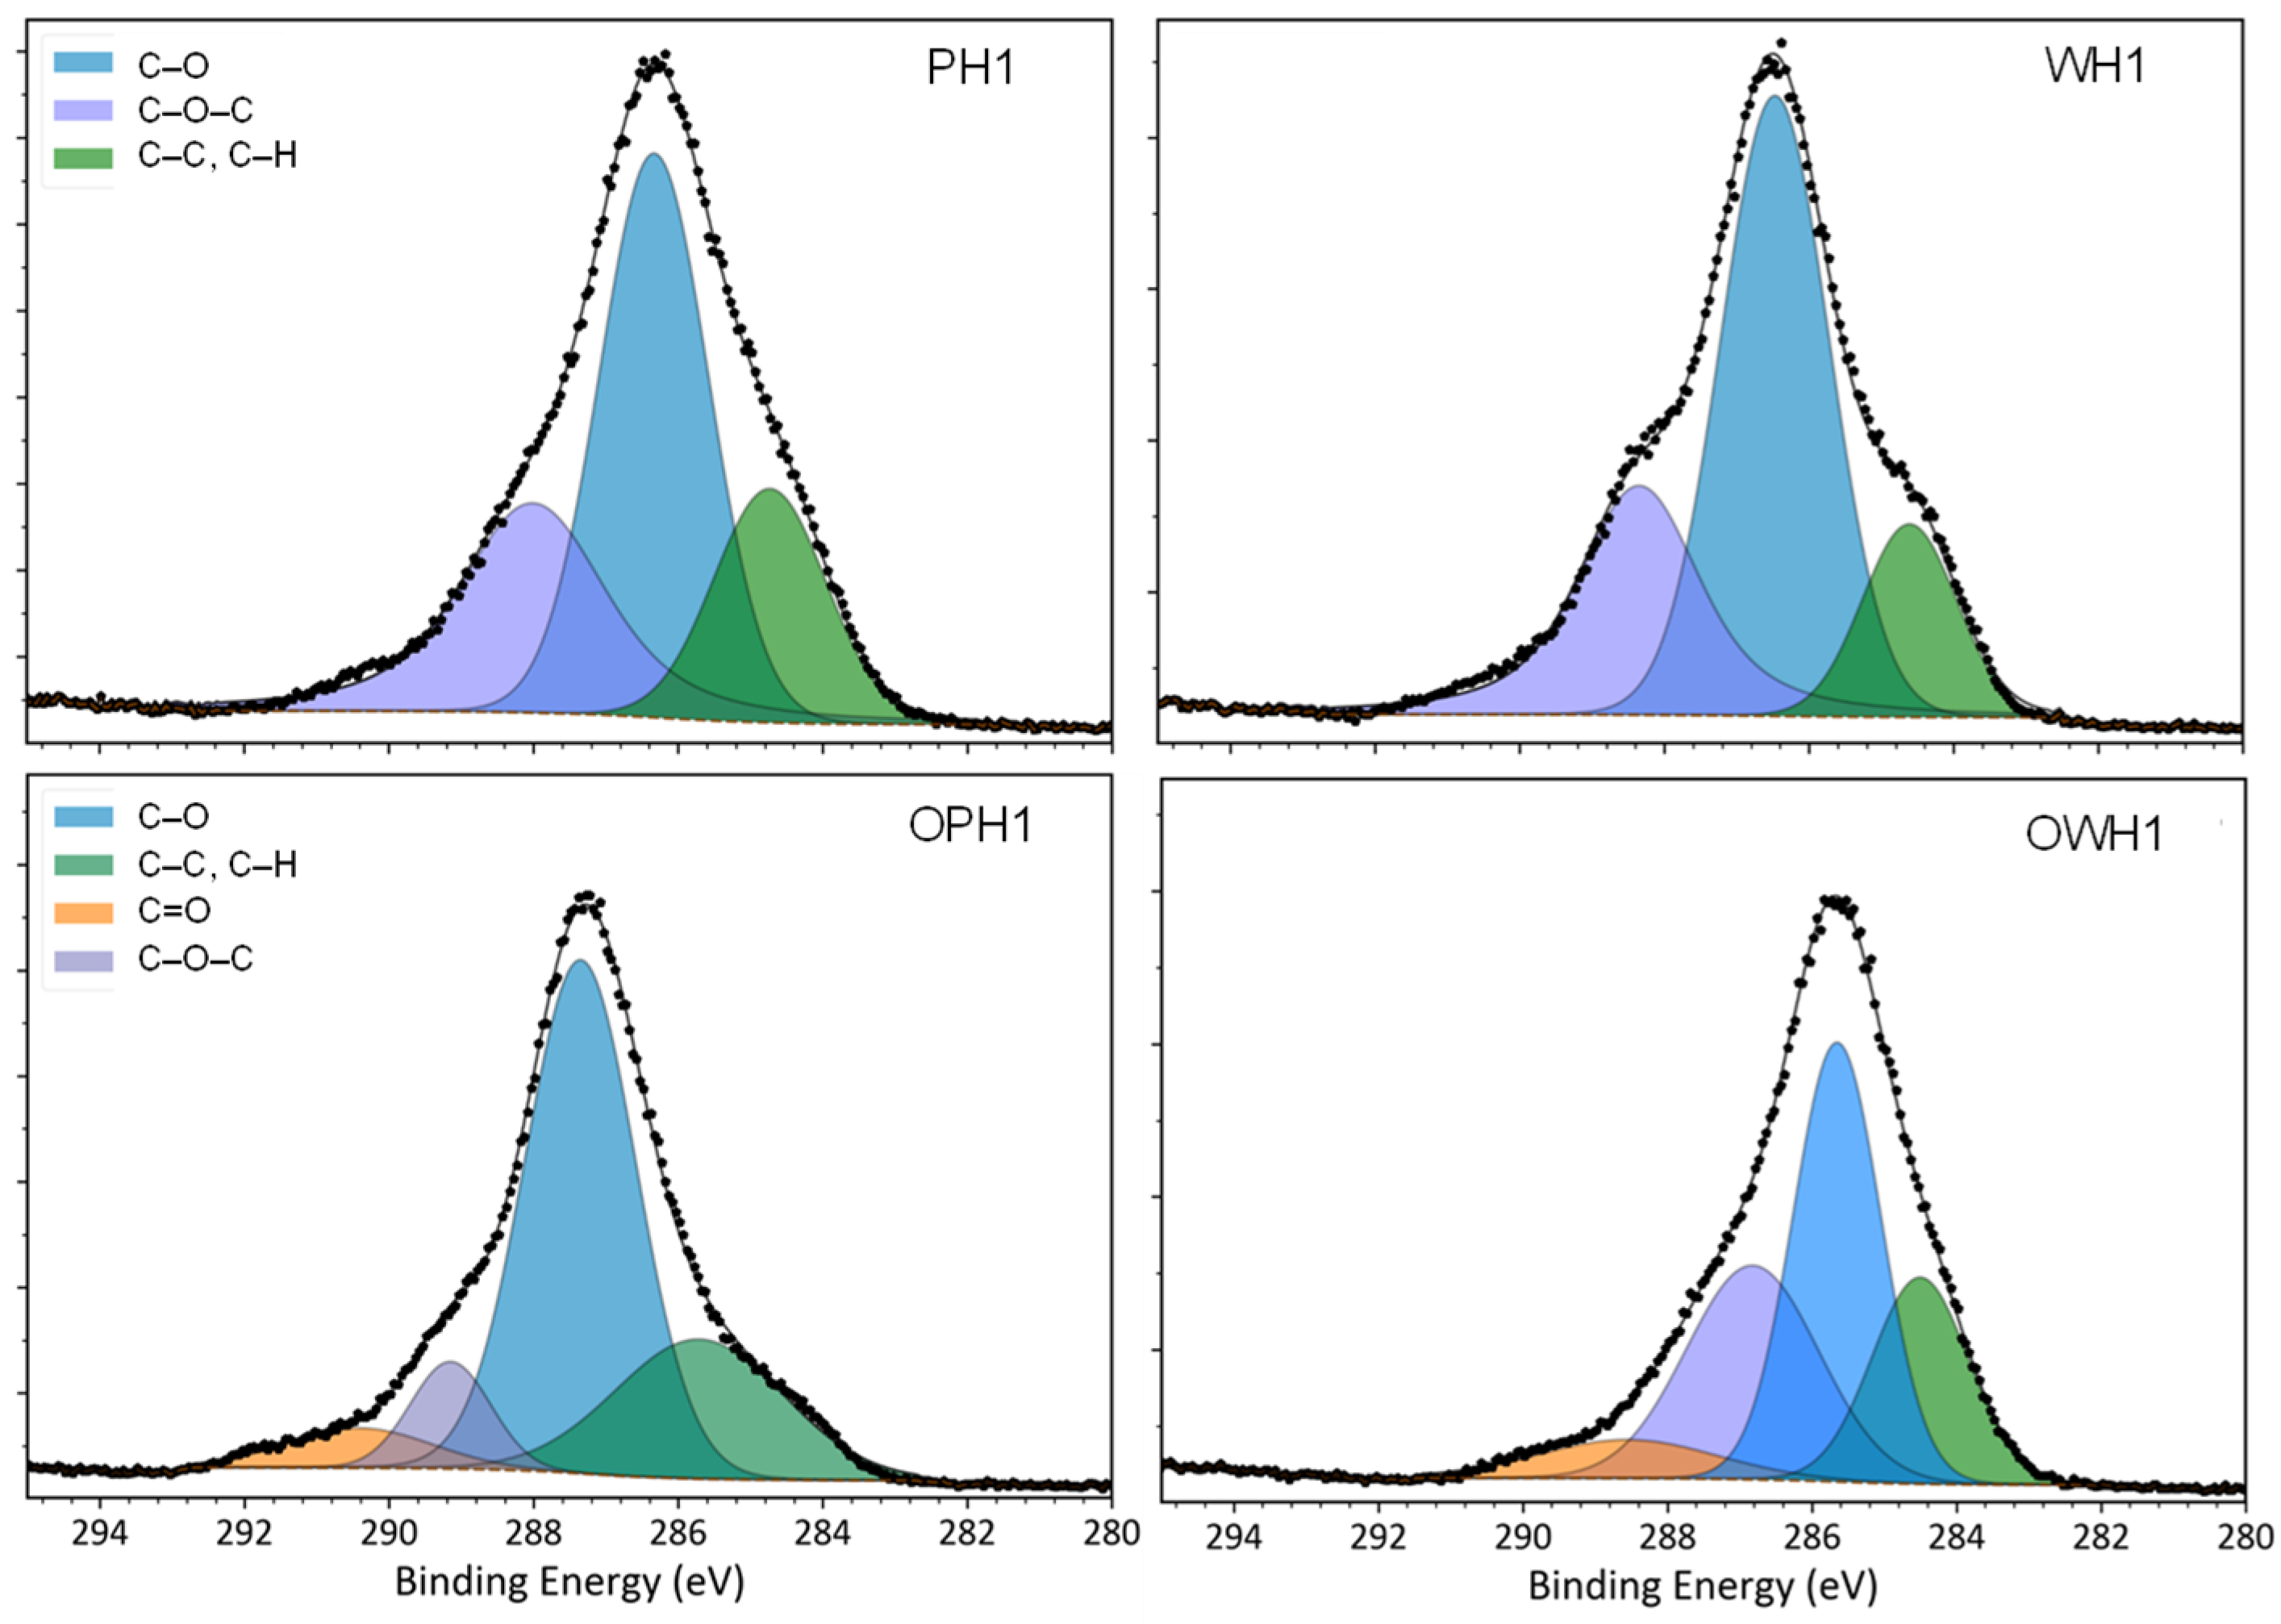
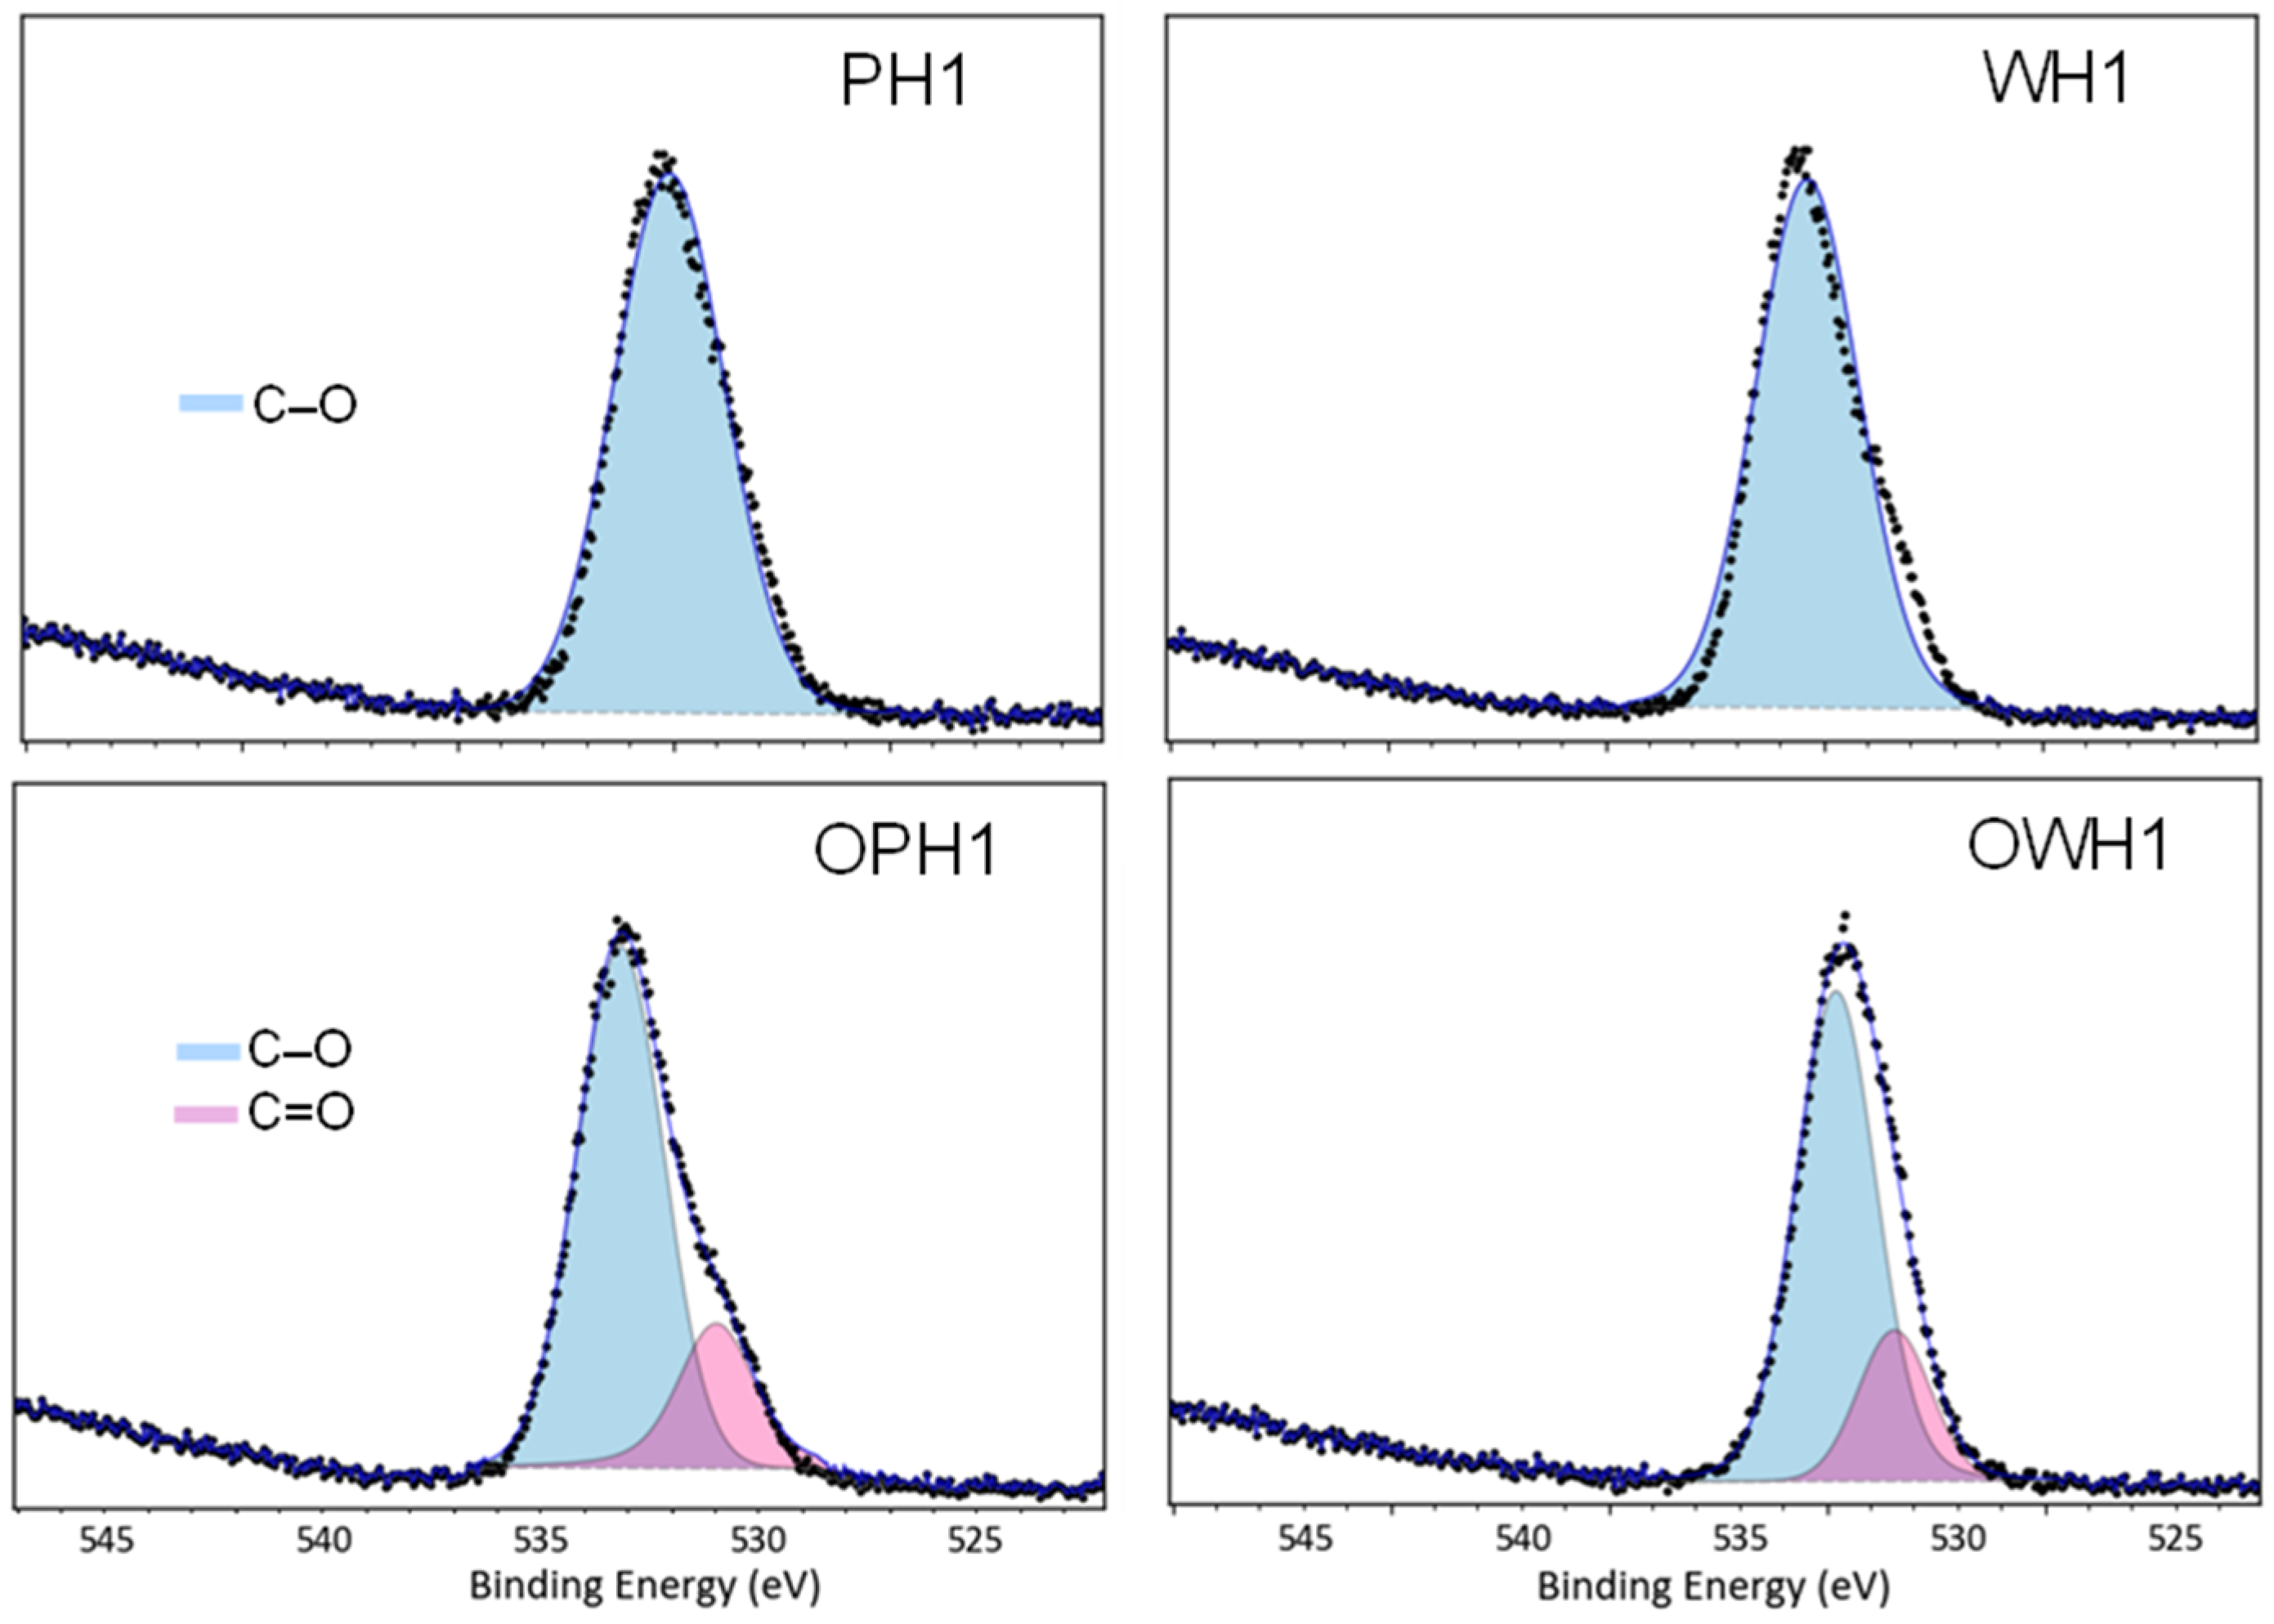
The surface chemical composition was assessed using an X-ray photoelectron spectrometer (K-Alpha, Thermo Fisher, Waltham, MA, USA) with an excitation source of Al Kα X-rays (hv = 1486.6 eV), a current of 16 mA, and a voltage of 12 kV. The spot size was 300 µm, where full spectrum data were acquired at a passing energy of 100 eV with a resolution of 0.5 eV, whereas the high-resolution spectrum was obtained at a passing energy of 20 eV with a resolution of 0.05 eV [
2]. The XPS spectrum was corrected with C1s = 284.80 eV binding energy as the energy standard. Open-source KherveFitting software (version 1.5) was used to process data.
2.6.2. Water Solubility and Absorption Indexes
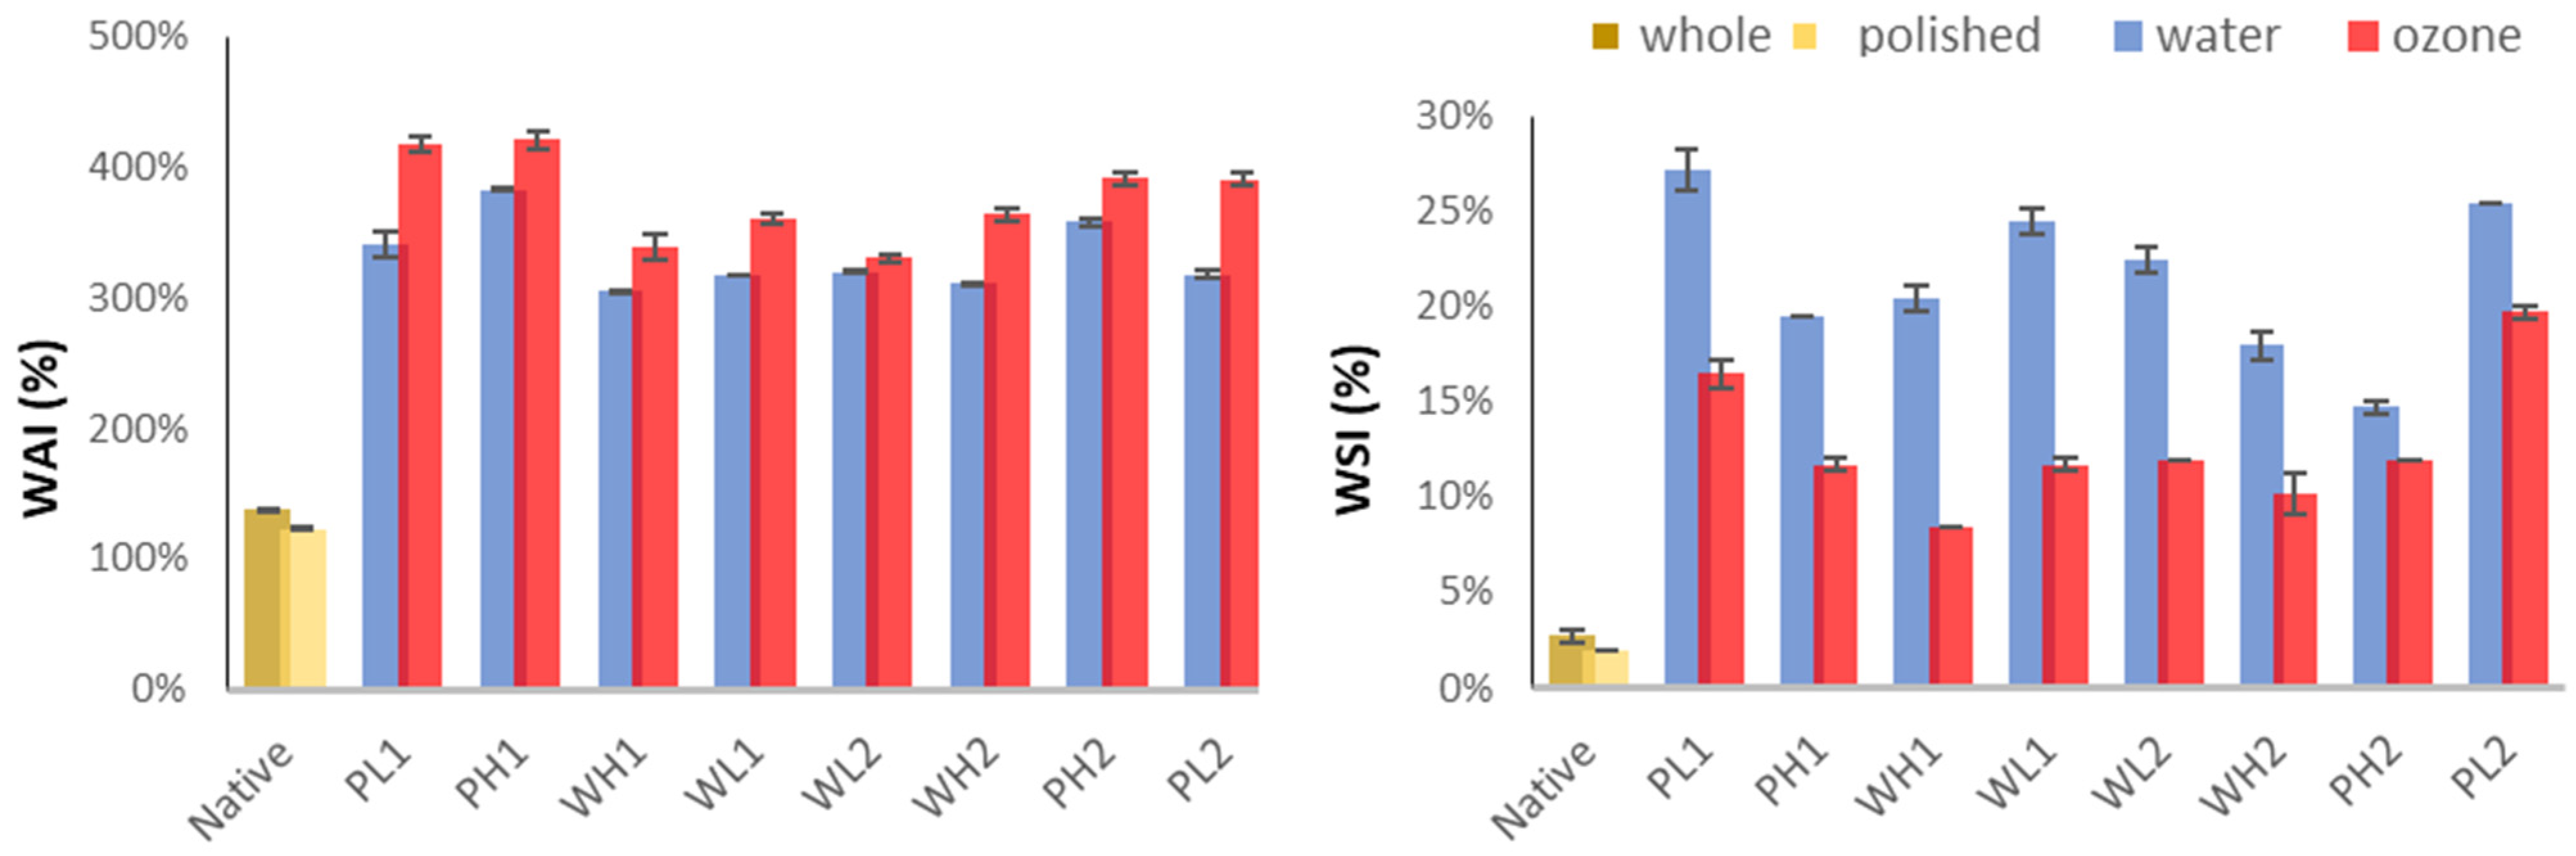
Water solubility (WSI) and absorption (WA) indexes of flour were determined following the method of Palavecino et al. [
16], with slight modifications. Briefly, 2.0 ± 0.1 g (db) was weighed for each sample in 50 mL centrifuge tubes and was suspended in 25 mL of distilled water. The mixture was vortexed vigorously and then oscillated for 30 min. Subsequently, the samples were centrifuged at 3500 rpm for 20 min and the supernatant was transferred to a Petri dish and dried in an oven at 55 °C with an air velocity of 4 m/s for 24 h. Once dried, the Petri dish was weighed to determine the difference from the empty dish, and the result is expressed as grams of dried supernatant per gram of sample, thereby obtaining the WSI. The pellet was weighed, and the WA was expressed as g of absorbed water by g of sample. Determinations were performed in triplicate and expressed as the mean.
2.6.3. Color
The color of native flours and milled extrudates was determined following the method described by Palavecino et al. [
16] with a colorimeter (CM-600d; Konica Minolta, Tokyo, Japan) using a D65 illuminant at 10° observation. A quantity of approximately 3 g of flour was placed on a flat, white surface and covered with 0% reflectance glass. The colorimeter was then positioned at the center of the glass to obtain measurements expressed in the CIELAB scale (L*, a*, b*). The total color difference ΔE was calculated as Equation (2).
where the subscript
W refers to the sample without ozone treatment and
O refers to the ozonized ones. This parameter was calculated to assess the effect of the oxidizing power of ozone bleaching extruded flour.
2.6.4. Viscosity Profile
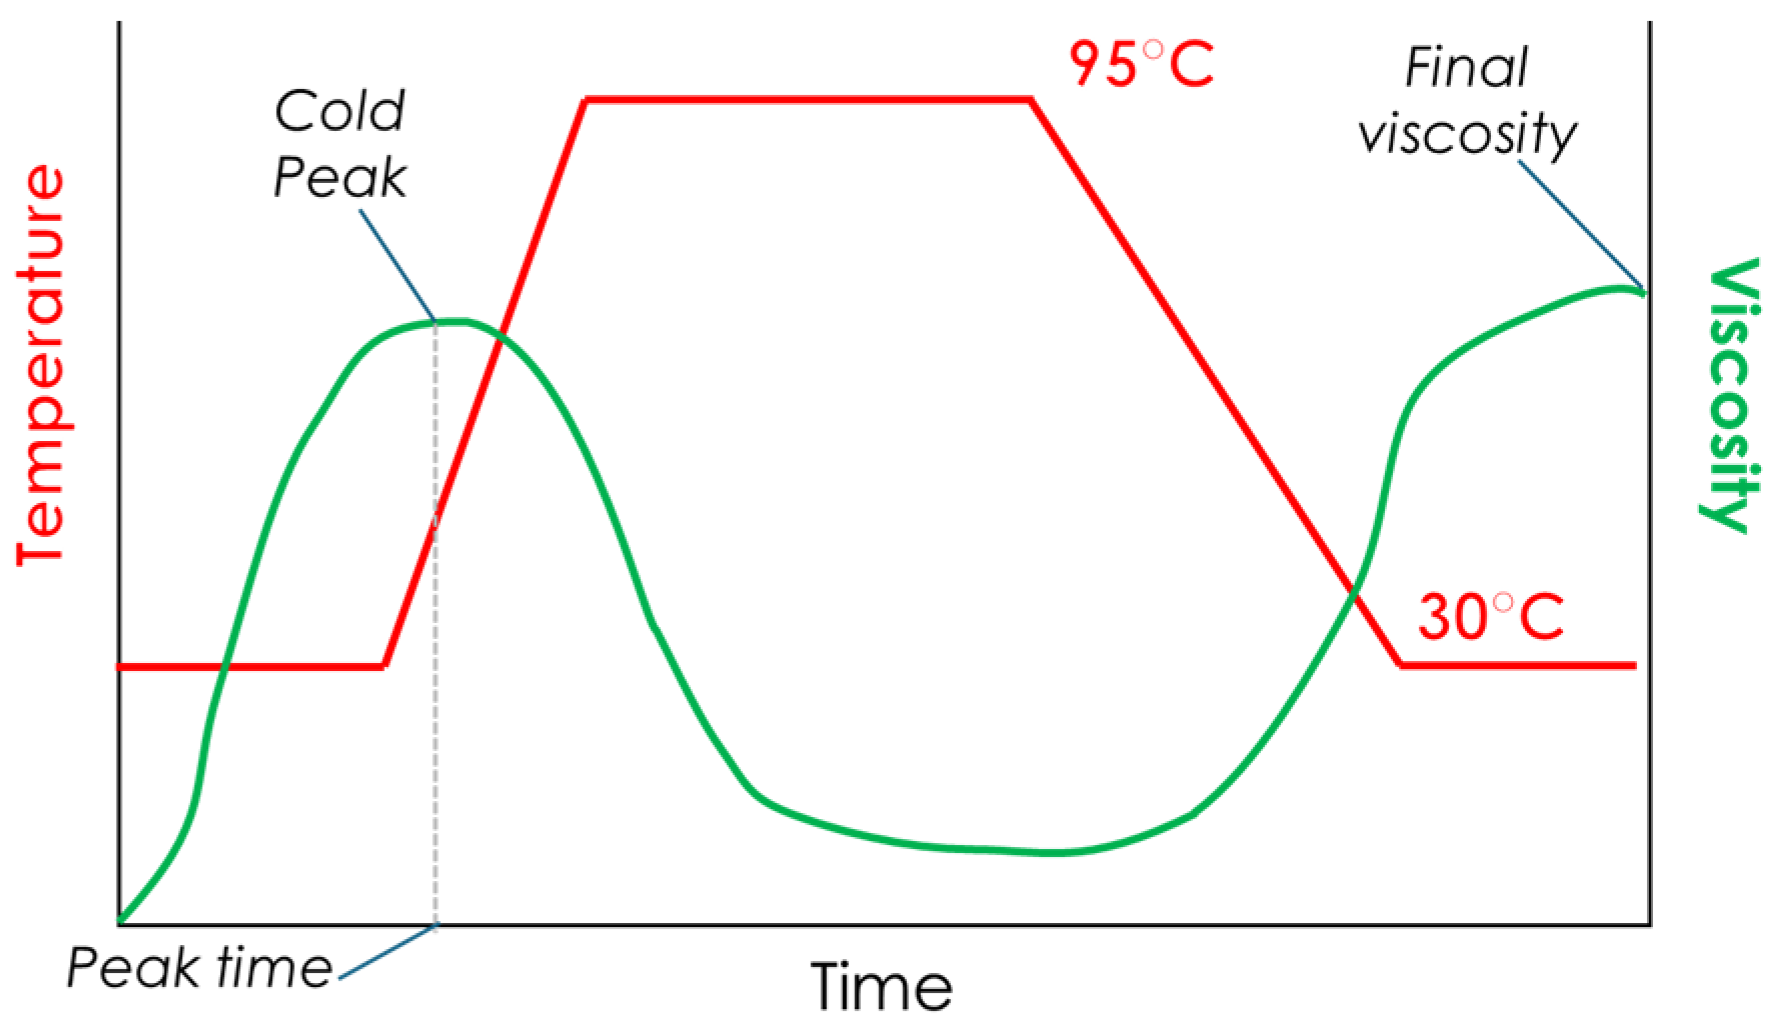
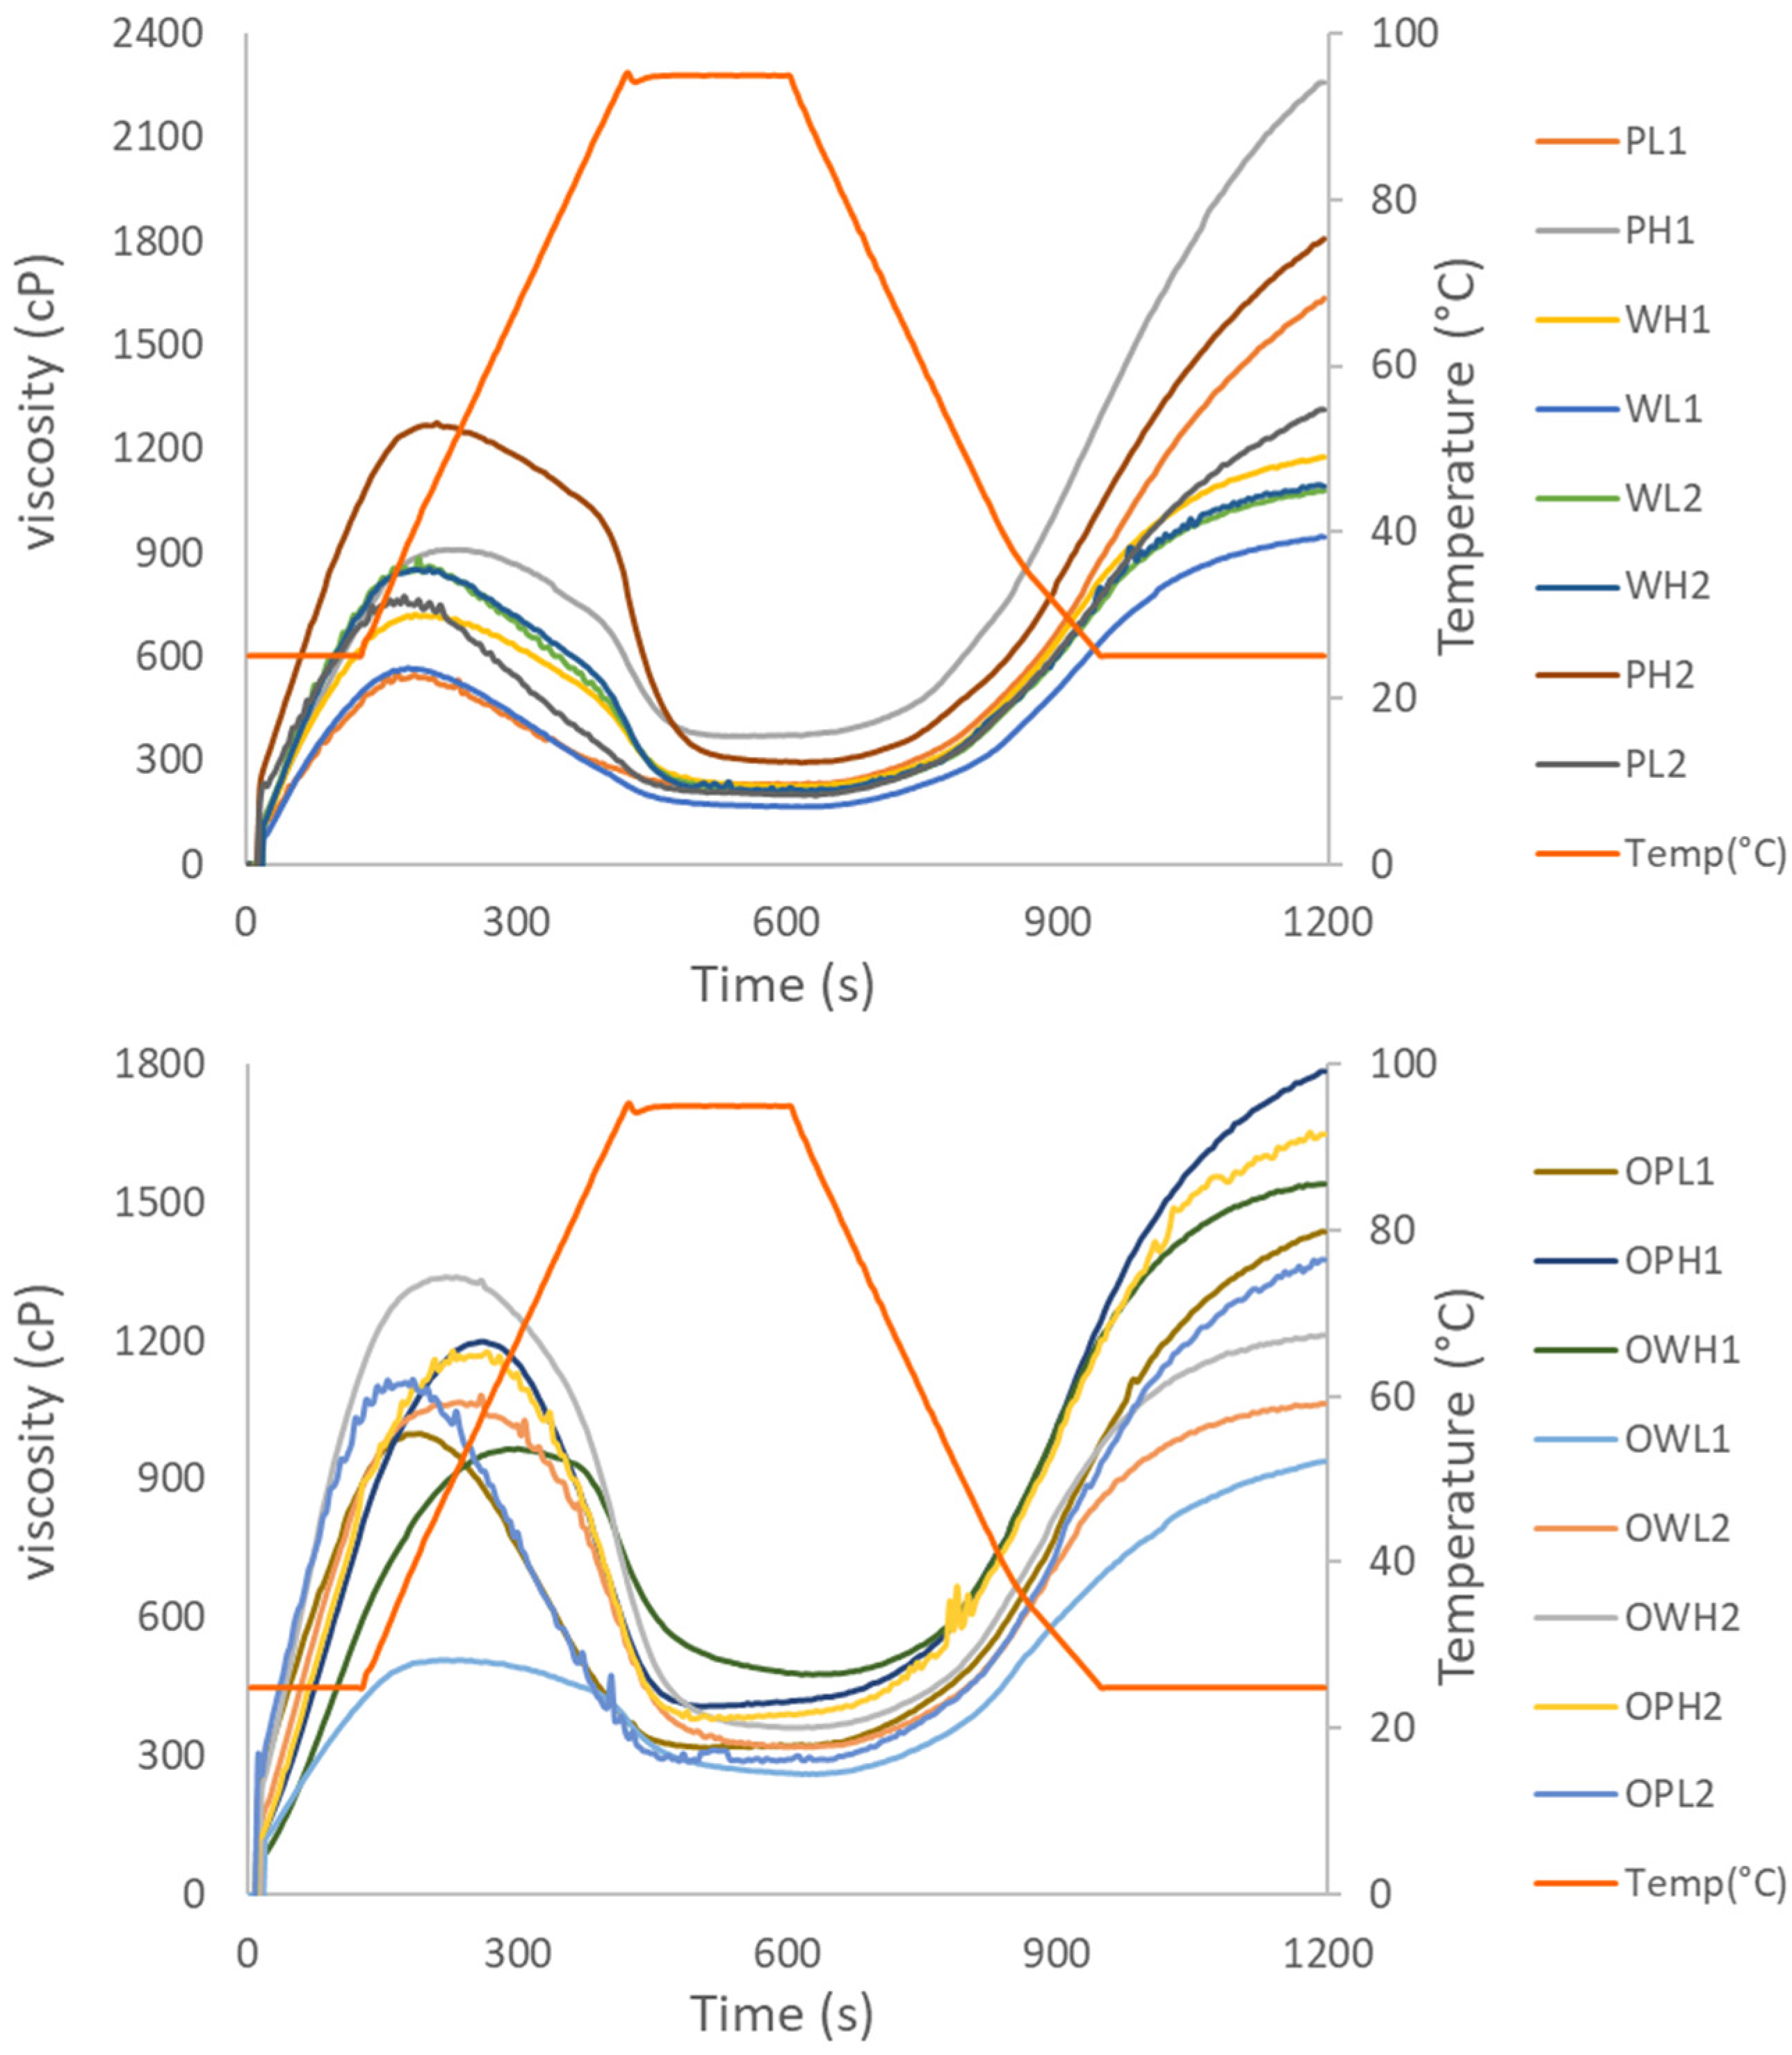
The pasting properties were determined using a Rapid Visco Analyzer (RVA 4500, Newport Scientific, Warriewood, Australia) following the pregelatinized starch method, a procedure included in the software Thermocline (version 3.17, Perten, Macquarie Park, Australia), with slight modifications. Briefly, 5.00 ± 0.01 g of flour was weighed in a canister and 2.00 ± 0.01 g of castor sugar was added and thoroughly mixed. Then, 25.0 ± 0.1 mL of cold (15 °C) distilled water was added to the solids. The temperature profile began at 30 °C and was kept for 2 min. The temperature then increased to 95 °C and was held constant for 3 min, after which it decreased back to 30 °C until the conclusion of the assay (
Figure 1). The RVA analysis quantifies starch pasting behavior via parameters such as cold peak (CP), final viscosity (FV), and peak time. These metrics assess starch quality and functional properties relevant to food processing applications.
The cold peak (CP) is defined as the maximum viscosity recorded at the onset of the RVA extruded flour test, when the sample is kept at a low temperature. This measurement reflects the starch’s capacity to hydrate under cold conditions. A high CP value suggests that the starch quickly absorbs water, which is characteristic of a high level of starch pre-gelatinization. In native flours, the cold peak corresponds to the viscosity point where most of the starch granules have swollen to their fullest extent while staying structurally intact. This marks the beginning of the gelatinization process. For extruded flours, the CP refers to the cold viscosity peak, as these flours have already undergone starch pre-gelatinization during extrusion, resulting in altered starch granules.
Final viscosity (FV) refers to the capacity of a material to develop a viscous paste or gel after cooking and cooling, and it is considered the primary parameter for assessing the quality of starchy products. Enhanced interactions among amylose molecules or hydrolysates of comparable length led to increased resistance to flow, resulting in higher system viscosity.
2.7. In Vitro Digestion Using Static Method
In vitro digestion of the extrudate samples was performed in duplicate according to Bustos et al. [
17] to evaluate starch hydrolysis. This method is based in the highly recognized standardized static method proposed by INFOGEST [
18]. Briefly, the ratio used was 50/50
w/
v for sample/Simulated Salivary Fluid (SSF), oral content/Simulated Gastric Fluid (SGF), and gastric content/Simulated Intestinal Fluid (SIF) corresponding to three stages: oral, gastric, and intestinal.
2.7.1. Starch Digestibility
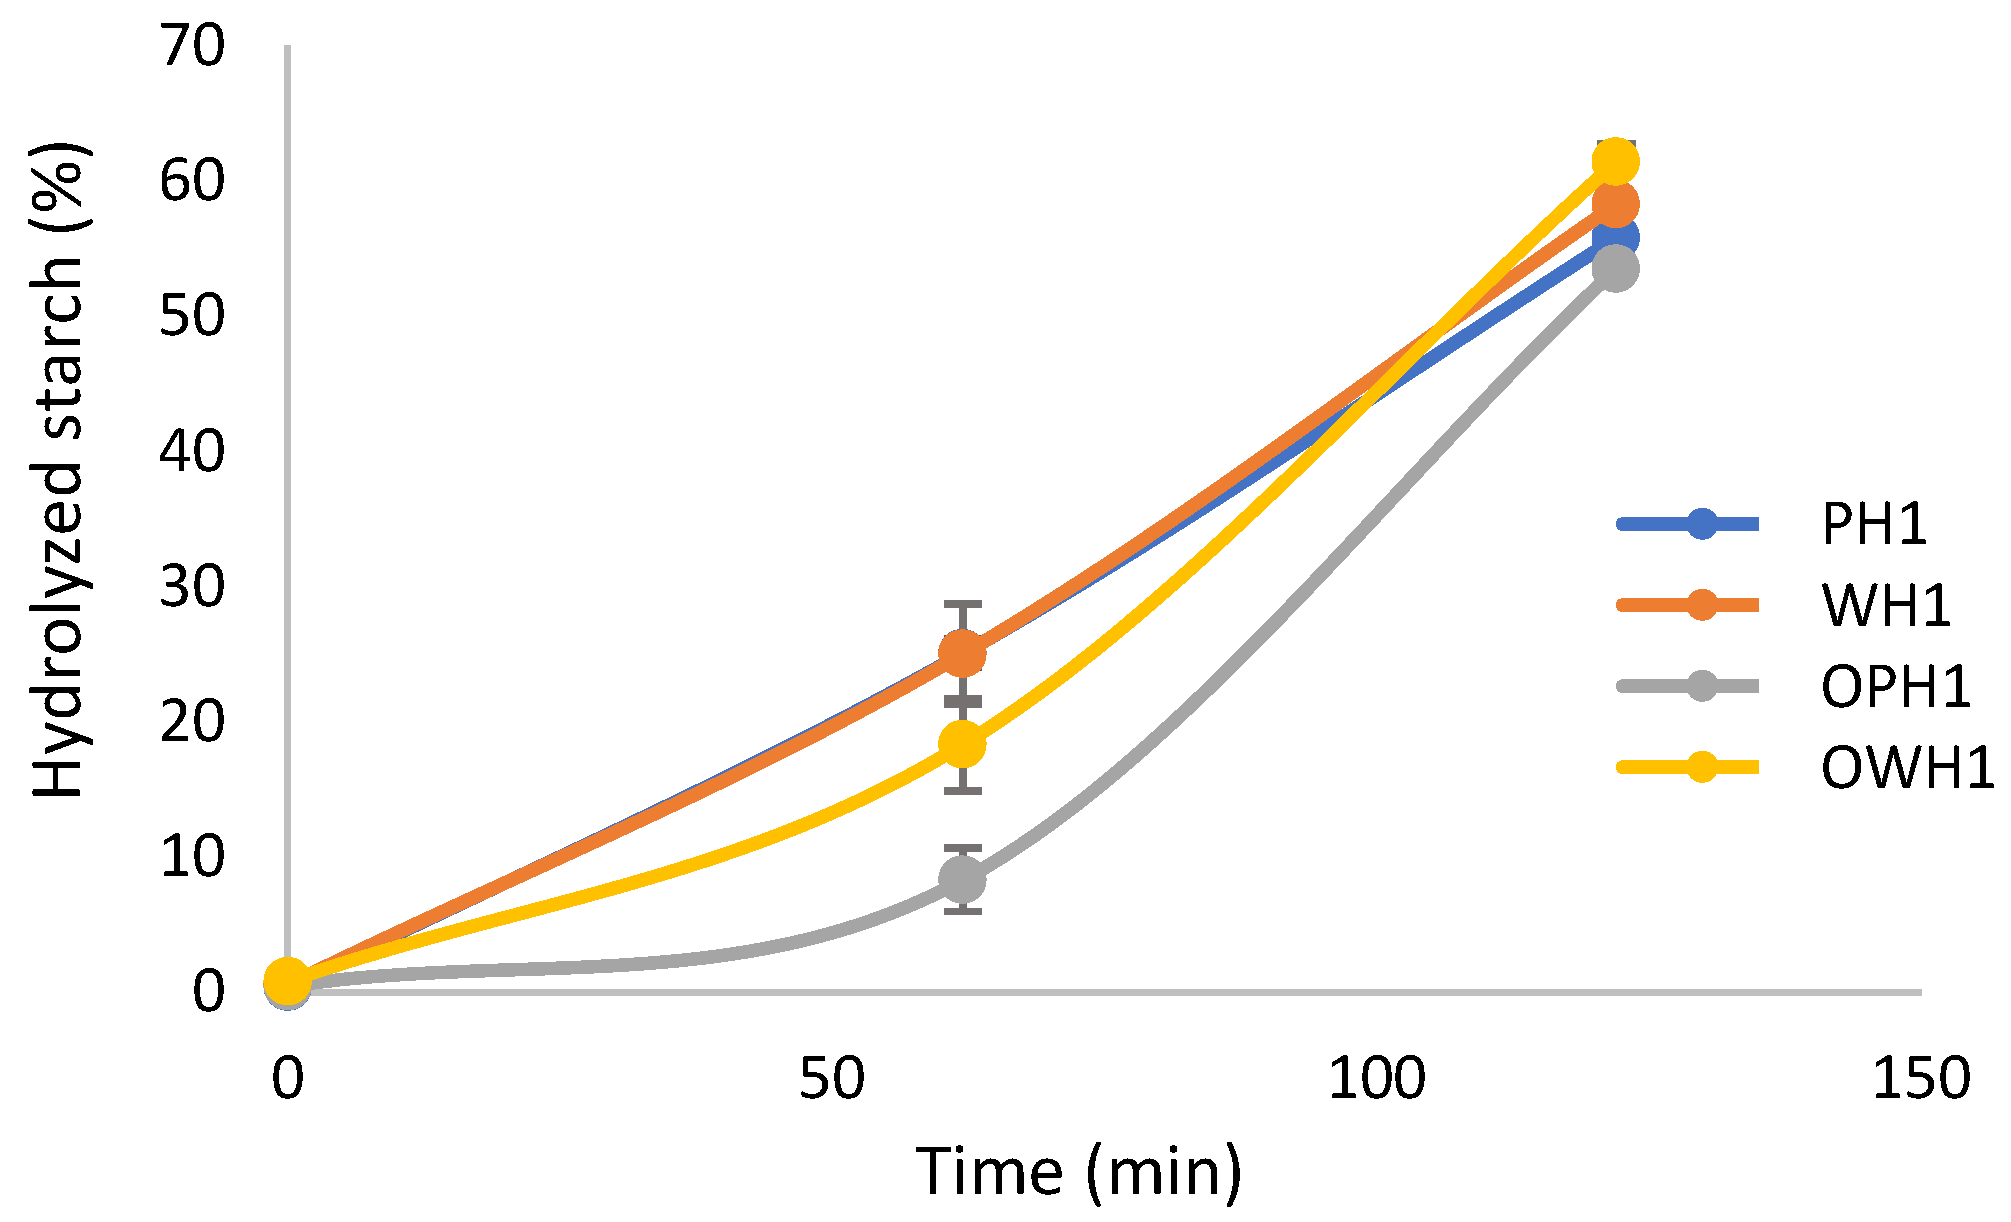
During in vitro digestion, aliquots of 1 mL were withdrawn at time 0, after oral digestion, after 120 min of the gastric phase, and at the end of the intestinal step (another 120 min) to monitor the hydrolysis degree of starch and its kinetic parameters. Starch hydrolysis was monitored by an analysis of reducing sugar content in each aliquot using the 3,5 dinitrosalicylic acid (DNS) method.
2.7.2. Quantification of Free-Amino Groups (OPA Method)
Free amino groups in the supernatant from the digests were measured using the o-phthaldialdehyde (OPA) method according to Nielsen et al. [
19] and used OPA reagent (P1378, Merck KGaA, Saint Louis, MO, USA) and serine as standard and deionized water for blank value. The results were expressed as absolute values of serine equivalents in 0.5 g of proteins corresponding to digested samples.
2.8. Statistical Analysis
Analyses of variance (ANOVA) with multiple comparison tests (DSG, α = 5%) were conducted using InfoStat software (Version 13p), and the artwork was created in Excel (Microsoft 365 version).
4. Conclusions
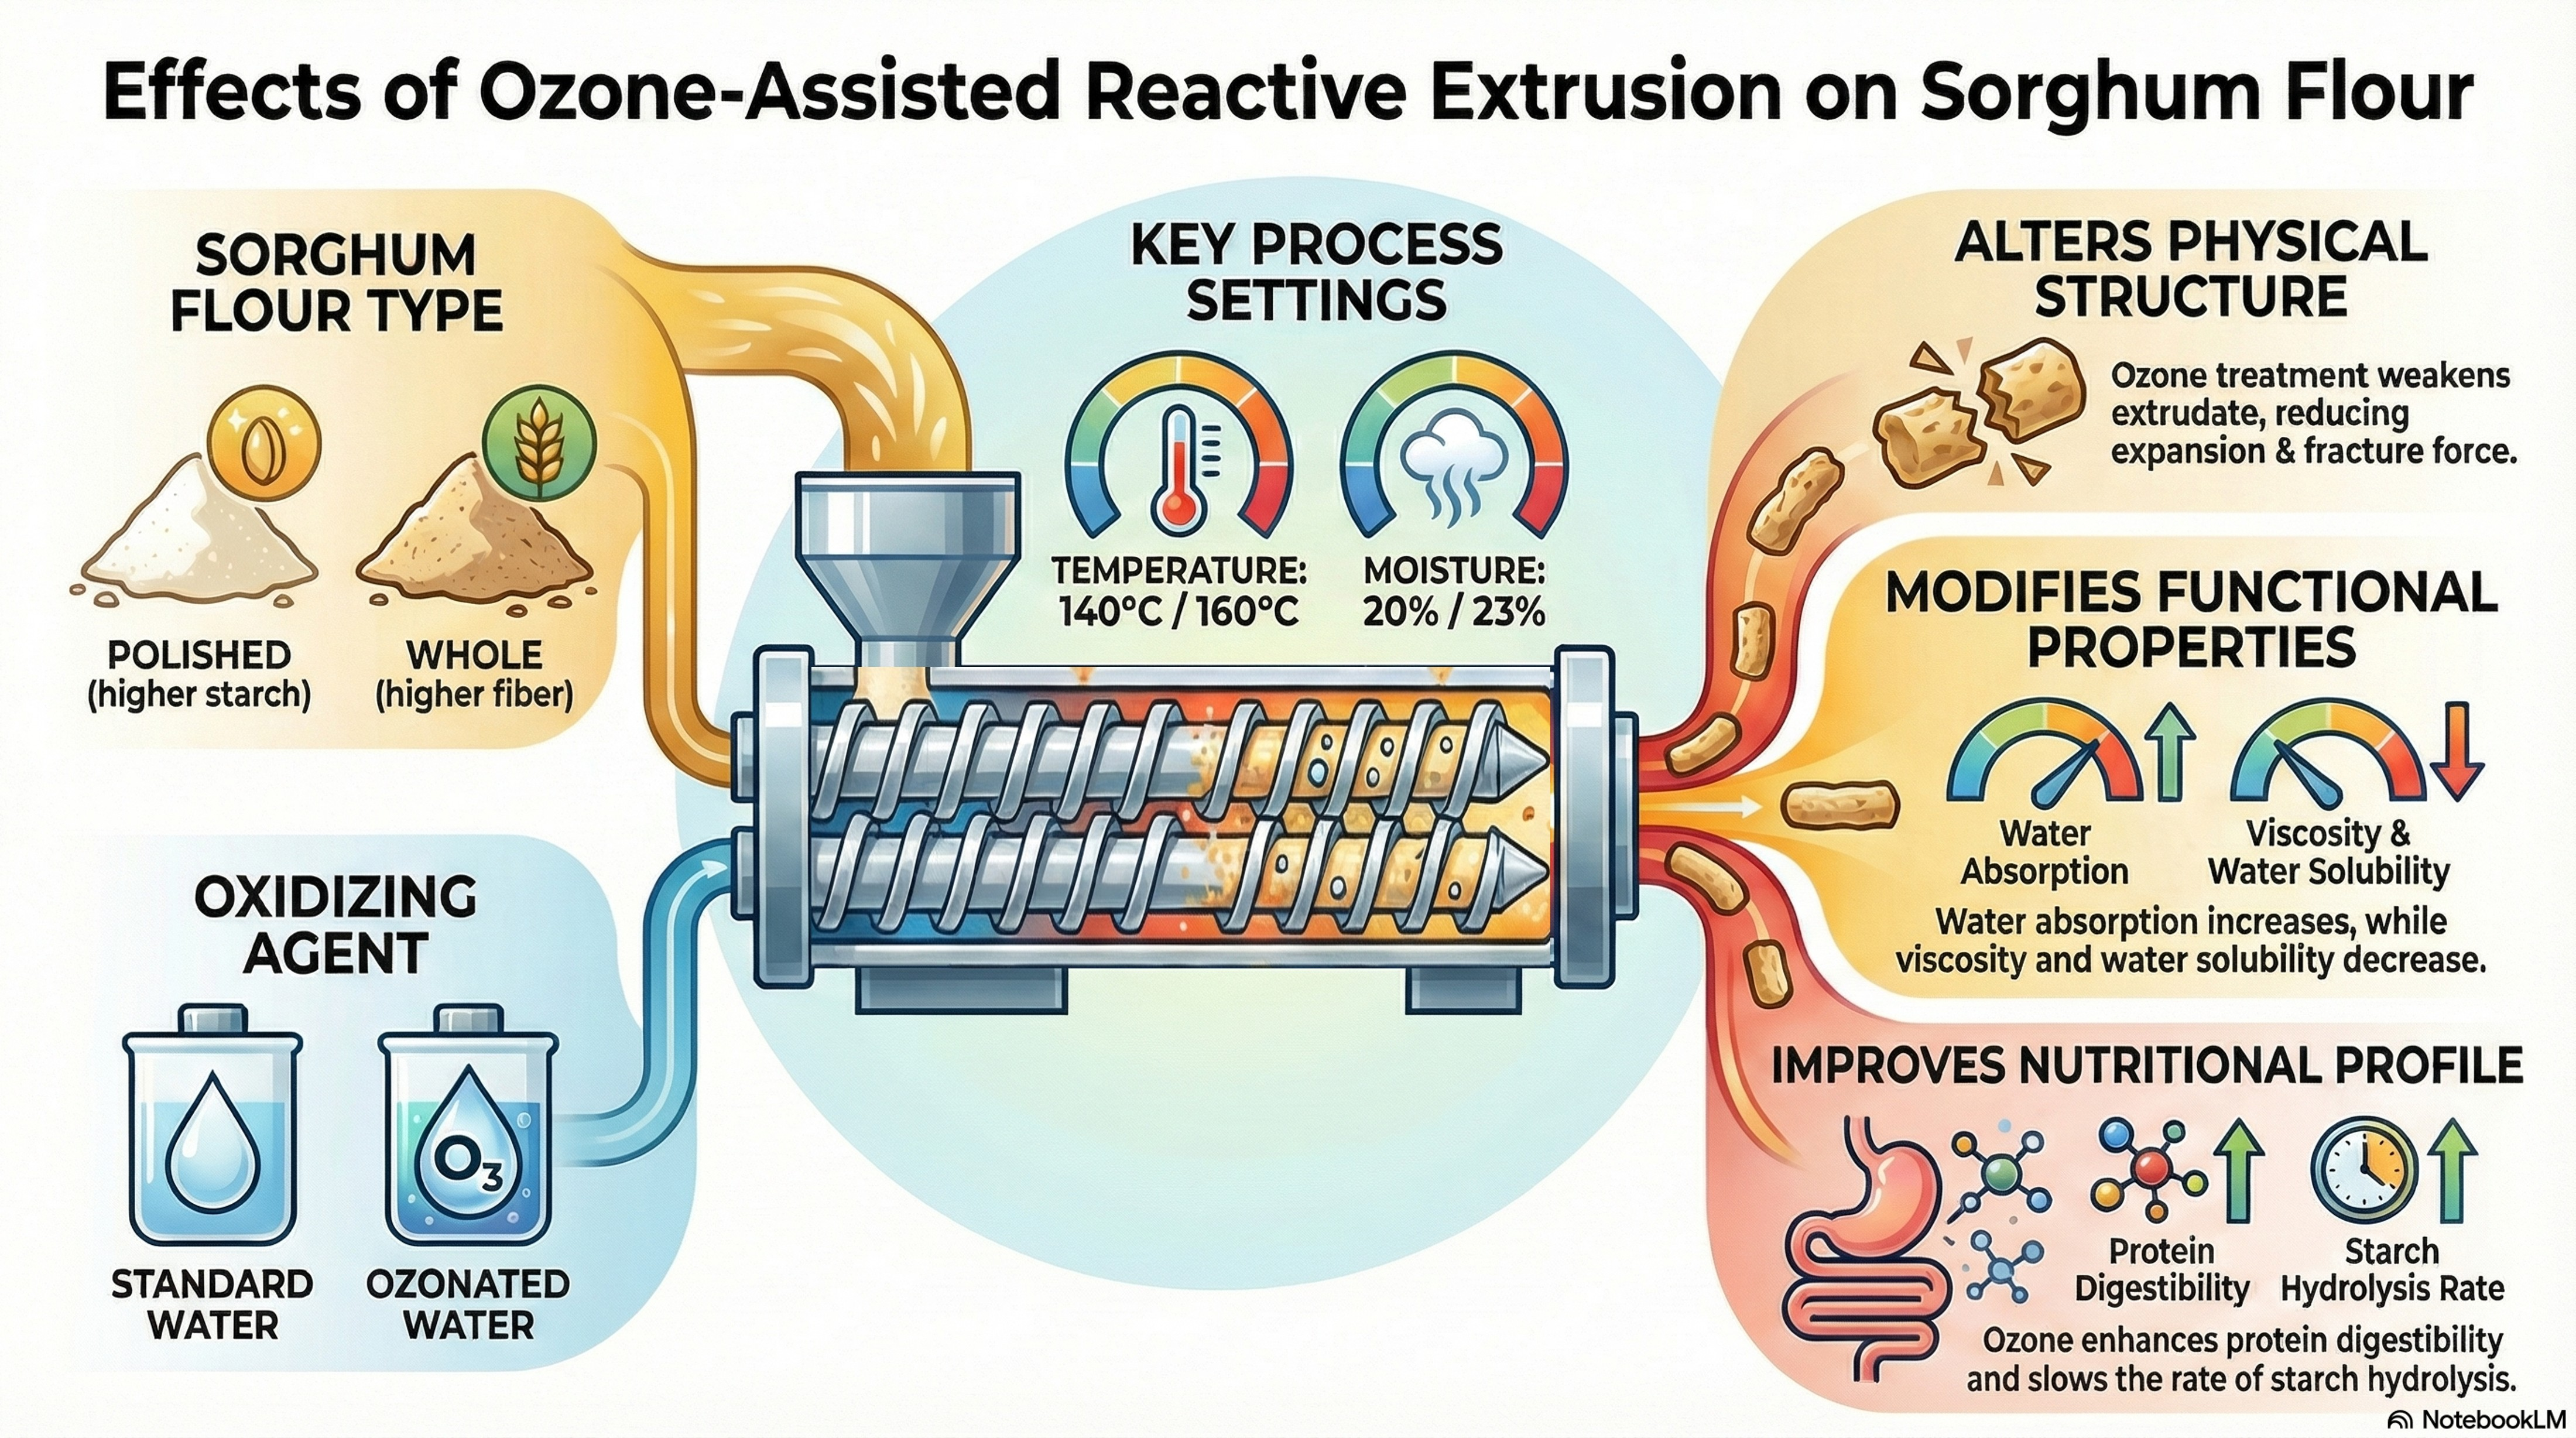
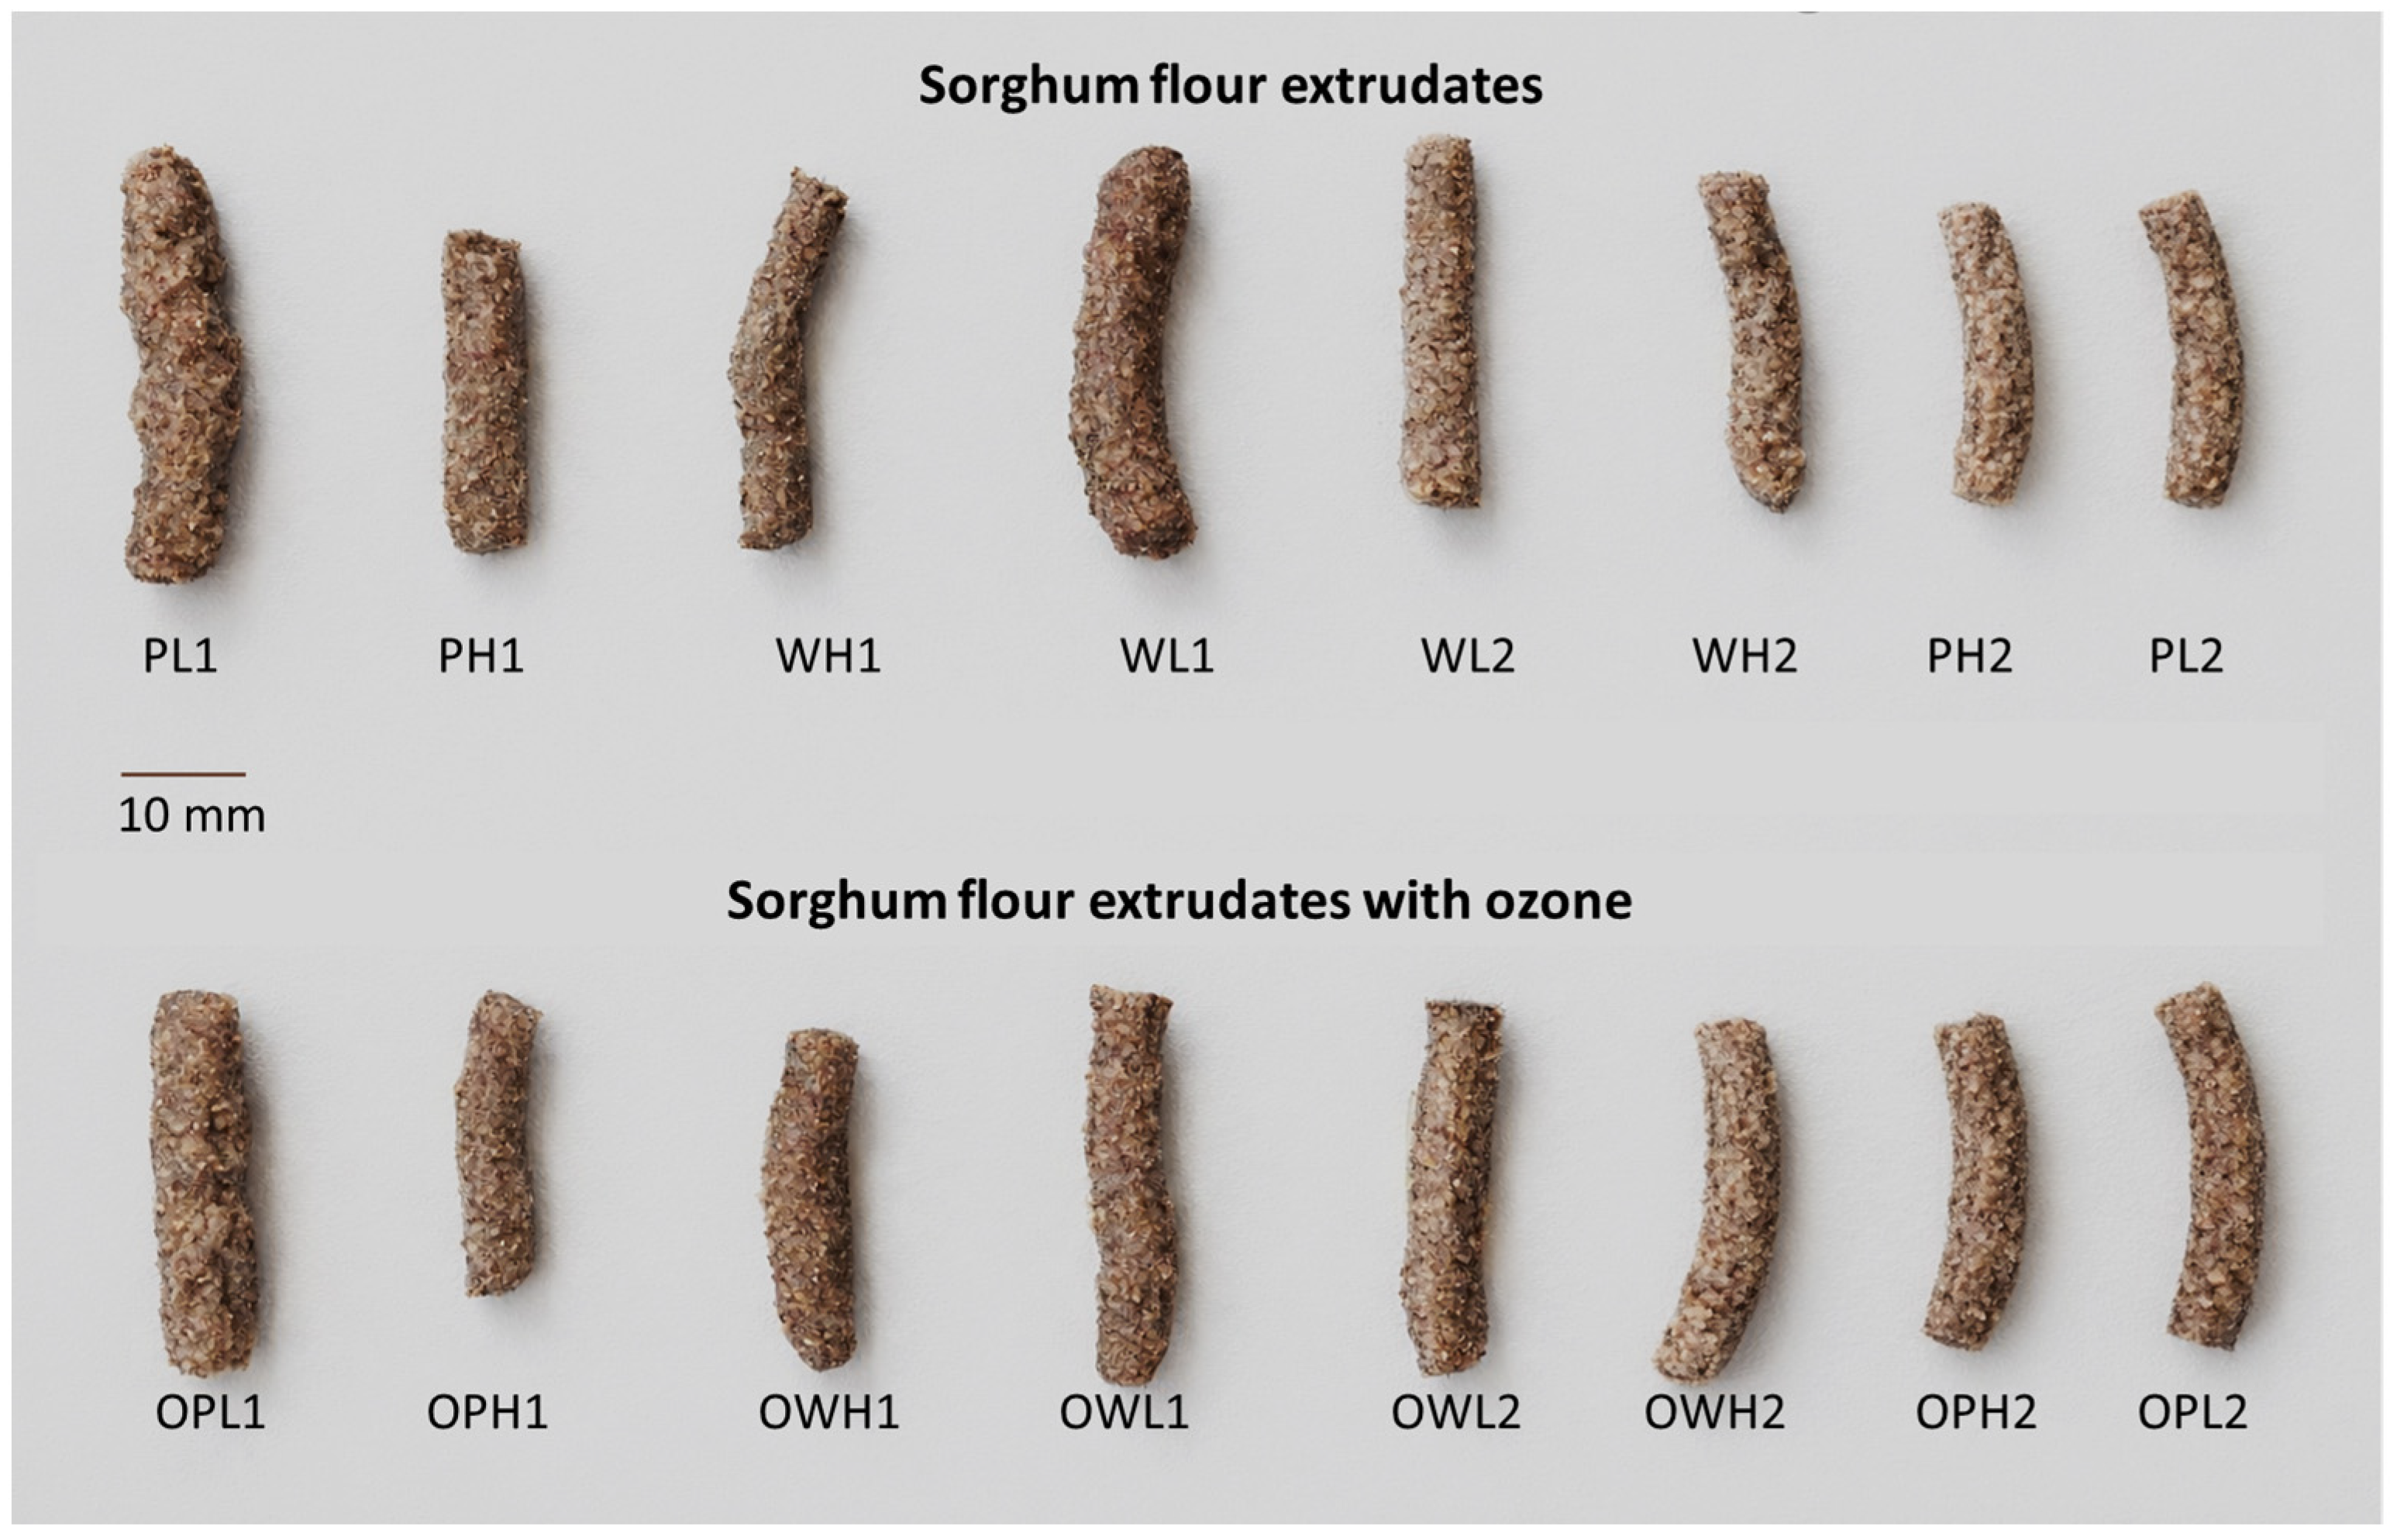
The reactive extrusion carried out with a twin extruder coupled with saturated ozone solution in feed water significantly changes the extrudate and resultant flour properties. Extruder process parameters were affected, and conditions for minimal SME involved the ozone-assisted extrusion of polished flour at elevated temperatures (160 °C) and higher water flow rates, whereas whole flour benefited from lower temperatures (140 °C) to balance energy input and functional properties. Ozone treatment alters the structure of extrudates, especially in polished flour, where it increases density but decreases expansion and fracture force. These changes occur due to starch degradation and diminished polymer interactions, which weaken the extrudate.
Water-related functional properties were also changed with ozone addition and visibly governed by starch accessibility and structural modifications. Ozone improved WAI but reduced WSI by promoting aggregation, whereas whole flour fiber content restricted solubility. Higher temperatures and ozone presence promoted starch degradation, reducing viscosity profile parameters, but less of an effect was observed in whole flours. In vitro digestion results indicate that ozonation improved protein digestibility while also decreasing the rate of starch hydrolysis in extruded samples, especially in the early stages.
Sorghum extrudates developed in this research differ from extrudate products available on the market mainly because commercial products are characterized by high and fast starch digestibility, low protein content, and high fracture force. Future work should focus on the sensorial analysis and in vivo bioavailability studies of extrudates.


 ,