Article

Numerical Analysis of High-Temperature Tensile and Compressive Creep in Cast Irons: Local Effects of Microstructure

by
Abhijit Joshi
,
Konstantinos P. Baxevanakis
and
Vadim V. Silberschmidt
*
Wolfson School of Mechanical, Electrical and Manufacturing Engineering, Loughborough University, Loughborough LE11 3TU, UK
*
Author to whom correspondence should be addressed.
Appl. Sci. 2026, 16(16), 7894; https://doi.org/10.3390/app16167894
Submission received: 26 June 2026 / Revised: 30 July 2026 / Accepted: 4 August 2026 / Published: 7 August 2026
(This article belongs to the Special Issue Applied Numerical Analysis and Computing in Mechanical Engineering)

Abstract

Cast irons are extensively used in high-temperature applications such as cylinder heads of heavy-duty diesel engines, where sustained exposure to high stresses and temperatures can initiate creep-related failure mechanisms, impacting their long-term durability and efficiency. Our previous experimental research demonstrated significant differences in creep mechanisms and behaviour of compacted graphite iron (CGI) under tensile and compressive loading. In situ analysis of the microstructural effects defining these differences during long-term high-temperature experiments is hardly possible. An alternative way to study these effects is to develop advanced micromechanical models using a finite-element method. The aim of this paper is to study the local responses at microscale (considering local distributions of stresses and strains) to macroscale long-term loading at high temperature employing direct introduction of microstructural features into numerical models. The models consider elasto-visco-plastic behaviour of the CGI material under tensile and compressive loading regimes. The novel results presented in this paper are applicable to cast irons as well as other heterogeneous materials such as metal matrix composites and the models presented can be used as a tool in the development of materials with microstructures customised for high-temperature applications.

1. Introduction

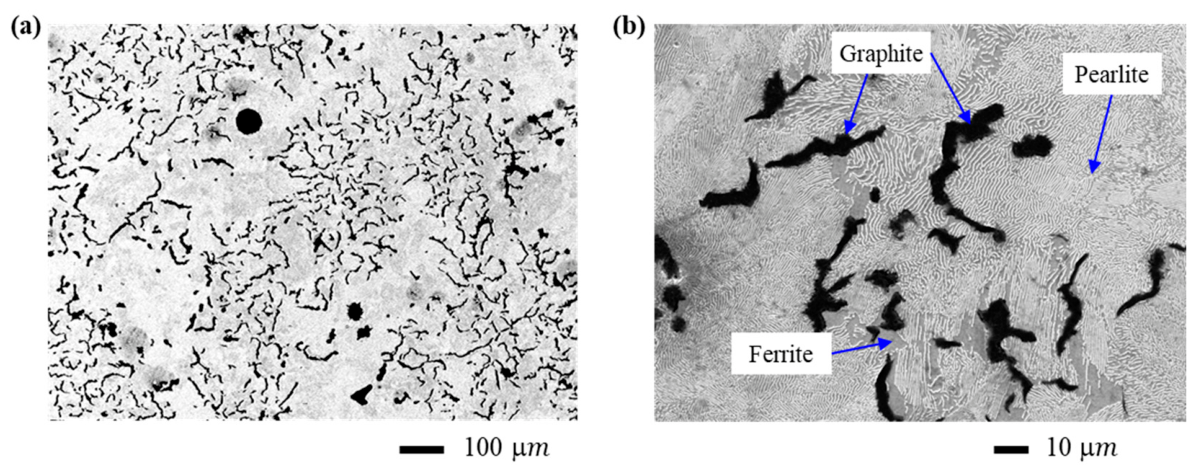
Compacted (or vermicular) graphite iron (CGI) has worm-shaped graphite particles embedded in the pearlitic or ferritic matrix (Figure 1). These particles with rounded edges are connected in three-dimensional coral-like formations within the matrix and have strong adhesion, resulting in improved tensile and fatigue strength compared to the traditional flake graphite iron (FGI) [1,2,3]. In FGI, the graphite particles are in the form of flakes with sharp edges, leading to the brittle behaviour with low tensile and fatigue strengths. Another commonly used cast iron is spheroidal graphite iron (SGI) with spherical graphite particles that make it more ductile and provide higher tensile and fatigue strengths at the cost of reduced thermal conductivity and castability. Commercial production of CGI only became possible in the late 1990s due to the need for precise control of magnesium, sulphur, and spheroidizing and anti-spheroidizing elements to ensure the required microstructure [4,5]. The microstructure and strength requirement of CGI are covered in different industry standards [6,7,8,9], which highlight the broad range of ferritic and pearlitic versions of CGI suitable for a wide range of applications.
The complexity and diversity of the graphite particle morphology in CGI is evident in the scanning electron microscopy (SEM) images (Figure 1). The material studied for this research was EN-GJV-450, which is a pearlitic form of CGI. The diversity of shapes and sizes of embedded graphite particles can lead to complex stress fields around them with a significant impact on the structural integrity of the products, in which this material is used.
Figure 1. SEM images of CGI microstructure: (a) diversity of graphite morphology; (b) graphite, ferrite and pearlite particles.
Applsci 16 07894 g001
Cast iron is extensively used in the cylinder heads of heavy-duty diesel engines. Traditionally, FGI was used to produce these parts, but with the drive for lighter and more efficient designs, the resulting increase in stresses and temperatures has led to CGI being considered a more suitable alternative [10,11]. Sustained exposure to high stresses at operating temperatures of 400 °C to 500 °C can lead to creep-related failure mechanisms that can have a detrimental impact on the long-term durability and efficiency of cast-iron parts [11,12,13]. Multiple studies on fatigue failure of these parts are reported in the literature [14,15,16,17,18,19,20] but detailed studies of creep in cast iron and, specifically, in CGI are rather limited [21,22,23,24]. Our recent paper [25] includes extensive experimental results for CGI highlighting the differences in creep behaviour and creep mechanisms governing the material response to tensile and compressive loading regimes. The paper also provided critical parameters necessary for numerical simulations of creep.
Cast iron is essentially a metal matrix composite (MMC) with soft graphite particles of various shapes and aspect ratios embedded in a pearlitic–ferritic matrix [26,27,28,29]. A wide range of MMCs are used where lightweight materials are required for high-temperature applications in automotive, energy and aerospace industries [30,31]. The advantage of MMCs is that they can be customised based on the requirements of specific application by addition and control of different reinforcements, as necessary. In such applications, insufficient understanding of the creep behaviour remains a limiting factor due to lack of established methods to evaluate the material’s creep response in high-temperature applications [32]. Several studies into low cycle fatigue, plasticity and creep are reported in the literature for MMCs [33,34,35,36] but—as in the case of cast iron—only a few are focussed specifically on the creep evolution in the material.
The thermomechanical analyses of cast iron published in the literature typically use phenomenological or micromechanical models [24,37,38,39,40,41,42]. In the former models, the overall macroscopic constitutive behaviour is captured, and the material parameters governing the macroscopic behaviour are experimentally determined. Such models cannot capture effects such as evolution of microstructure and dislocations [24,38,43]. Micromechanical models are necessary to understand the material behaviour under macroscopic loading at the microstructural level, e.g., local stress distributions around inclusions and the spatial evolution of plasticity and creep with time. Such micromechanical models can be helpful not only for cast irons but, in general, for any heterogenous materials such as MMCs.
This paper builds upon the results of our experimental work [25] and applies the experimental results in the finite-element-based micromechanical cell approaches to study the localisation effects in distributions of stresses and strains under long-term macroscopic loading at high temperatures. The models incorporate elasto-visco-plastic behaviour of the CGI material under tensile and compressive load regimes. The micromechanical models presented in this paper are based on a 2D representative-volume-element (RVE) approach, widely reported in the literature for cast iron [26,44,45]. The models are created in commercial finite-element software package Abaqus/CAE 2023.HF4. It is noted that CGI has complex 3D microstructural morphology and it is not possible to fully capture all effects of this microstructure using 2D models, but this study represents a starting point in the development of elasto-visco-plastic models for CGI. Our previous SEM studies demonstrated stability of CGI microstructure exposed to 500 °C for more than 100 h, thus removing the need to consider microstructural changes.
The literature review of microstructural simulations for cast irons shows different approaches used for modelling the graphite particles [27,44,45,46]. The two most common approaches used in the literature are (i) using voids instead of the graphite particles and (ii) modelling these inclusions as an isotropic solid [38,47]. The former approach represents a scenario with a complete loss of bonding between graphite and the matrix [48,49]; on the other hand, modelling the graphite as a solid reflects a case of perfect bonding between them. These two approaches are the two extreme cases of the graphite/matrix interface and provide upper and lower bounds for mechanical behaviours. The differences in the results obtained with these two approaches are compared for circular graphite particles.
The effect of graphite shape is investigated by comparing the results for idealised circular and elliptical inclusions followed by parametric studies on the effects of particle orientation and aspect ratio. The effects of realistic geometry of inclusions are also studied to understand the differences compared to the idealised geometries. The results from these studies provide a strong understanding of the effects of microstructure, specifically graphite morphology, on the high-temperature creep and plastic response of CGI. The developed models and the findings can be used as a tool for the development of improved materials with their microstructure optimised for specific high-temperature applications.
One of the limitations of the studies presented in this paper is that it does not account for the effects of adjacent particles. Such studies are reported in the literature [50] but they do not cover the creep effects analysed in this paper. Importantly, the fundamental approaches presented in this paper can be extended to account for multiple particles and realistic microstructures.

2. Materials and Methods

2.1. Creep Laws

Abaqus software [51] supports several creep laws such as strain- and time-hardening, time-power law, hyperbolic-sine law, etc. As reported previously [25], good fits were obtained for the test creep curves using the Bailey–Norton creep equation [52,53,54,55]:
ε c = A σ n t m
In this equation, the creep strain ε c is expressed in terms of stress σ and time t . The equation includes creep exponent n , and two other parameters, A and m , that are material- and temperature-dependent. The parameters n , A and m for the CGI material used in the current research are reported in our previous work [25]. The Bailey–Norton equation can be rewritten in the form of creep strain rate ε ˙ c with the same parameters n , A and m [52,55]:
ε ˙ c = m A σ n t m 1
The time-hardening creep-rate equation (Equation (2)) can be modified to eliminate the time factor [52,55]:
ε ˙ c =   m A 1 m σ n m ε c ( m 1 ) m
Equation (3) is known as the strain-hardening law, where the creep strain rate does not depend on time but is a function of stress and creep strain. In constant-stress scenarios, the time- and strain-hardening laws are equivalent [56]. However, under variable loading, experimental results show a better correlation with the strain-hardening law [56,57,58].
The time-hardening law available in Abaqus [51] is
ε ˙ c = C q n t p
It is noted that Equations (2) and (4) are similar, and they represent the Bailey–Norton creep strain-rate equation in slightly different forms. The creep exponent n is identical in Equations (1)–(4). In Equation (4), the creep strain rate ε ˙ c is expressed as a function of uniaxial equivalent deviatoric stress q , time t , and the creep exponent n . Parameters C and p depend on the material and temperature. Comparing Equations (2) and (4), the following relationship can be established between the Abaqus simulation parameters and experimental results. The following equations are used for derivation of creep parameters C and p :
C = m A
p = m 1
These parameters were obtained from our creep experiments, so they are the same for strain- and time-hardening formulations. The analyses presented in this paper are based on the strain-hardening law because, even under constant external load, the local state of stress in the model with inclusions constantly evolves with time as creep progresses.

2.2. Properties of Graphite and Matrix Material
The models presented in this paper include the elasto-visco-plastic behaviour for the matrix and elastic one for graphite. The material studied was EN-GJV-450, which has a mostly pearlitic matrix. The elastic properties of matrix and graphite (when modelled as a solid) at 500 °C used in our simulations are shown Table 1. The Young’s modulus of the matrix was based on the high-temperature tests of bulk CGI material reported in our previous publications [23,25]. The Young’s modulus from these bulk-material tests was 125 GPa and falls within the 100 to 135 GPa range reported in the literature for pearlitic matrix [24,37,59]. All other properties from Table 1 are taken from the literature [59,60].
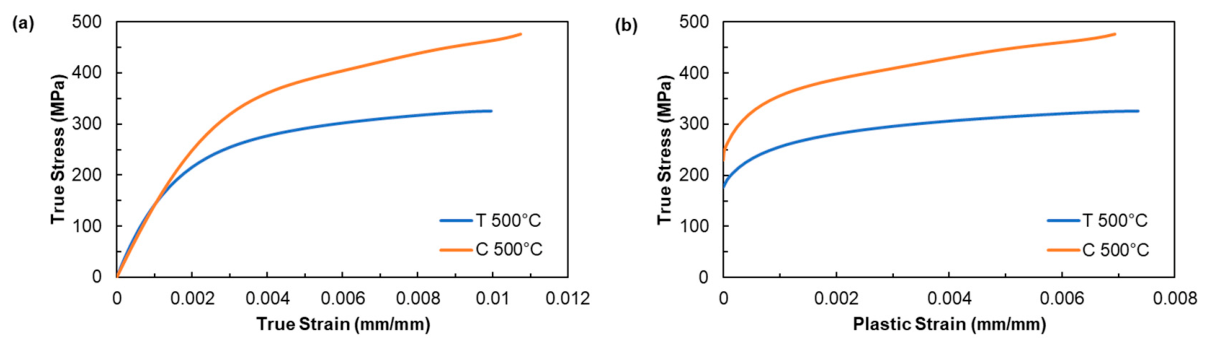
To consider the effect of plasticity for pearlitic matrix in the simulations, true stress vs. plastic strain curve should be provided as material data in Abaqus. There is not enough data in the literature to generate consistent tension and compression plastic material data for pearlite at 500 °C. To deal with this limitation, the data from bulk CGI material tests at 500 °C reported previously [23,25] was applied to the matrix. The engineering stress–strain curves for the tension and compression tests were first converted to true stress–strain curves (Figure 2a). The elastic strain was then subtracted from the true strain to obtain the plastic strain. The resulting curves of true stress vs. plastic strain are shown in Figure 2b and were applied to the matrix. Apparently, there is a considerable tension–compression asymmetry; at 500 °C, the tensile yield strength is 280 MPa and compressive yield strength is 380 MPa. The tensile strength of 280 MPa at 500 °C used in this paper for the pearlitic matrix is within the range of 240 MPa and 310 MPa reported in the literature [24,59,61]. Moreover, it is noted that the pearlite strength can vary significantly depending on the cooling rate, interlamellar spacing and the alloying elements [62,63]. A broad range of interlamellar spacing of the pearlitic matrix for the material used in this research is evident in Figure 1b.
The CGI matrix has a melting point of 1150 °C [4,21,64], and has a creep threshold of around 400 °C (i.e., homologous temperature of 0.47) as found in the experimental studies reported in the literature [21,22]. Graphite has an extremely high melting point of over 3000 °C [65,66,67] and does not show any creep behaviour at temperatures below 1000 °C [68]. As a result, the simulations in this paper do not include modelling of creep behaviour for the graphite particles. It is noted that in the presence of nuclear radiations and stresses, graphite can show signs of creep around 500 °C [69,70,71] but the effect of nuclear radiations is outside the scope of this work.
There are no published data in the literature specifically covering creep properties of the pearlitic matrix for tension and compression. So, the creep material properties derived from experimental results for the bulk CGI material published in our paper [25] were used for the matrix. This assumption was made because the creep process in CGI is driven by matrix deformation, while the effect of graphite is accounted for by modelling it as a deformable inclusion or as a void [21,72,73,74]. The creep simulation parameters C and p were obtained by substituting the experimental parameters in Equations (5) and (6). The full list of creep parameters from the experiments and those used in the numerical simulations for the matrix are shown in Table 2.
Figure 2. Plastic properties for CGI matrix at 500 °C: (a) true stress–strain curves; (b) true stress–plastic strain curves.
Applsci 16 07894 g002

2.3. Elements and Mesh

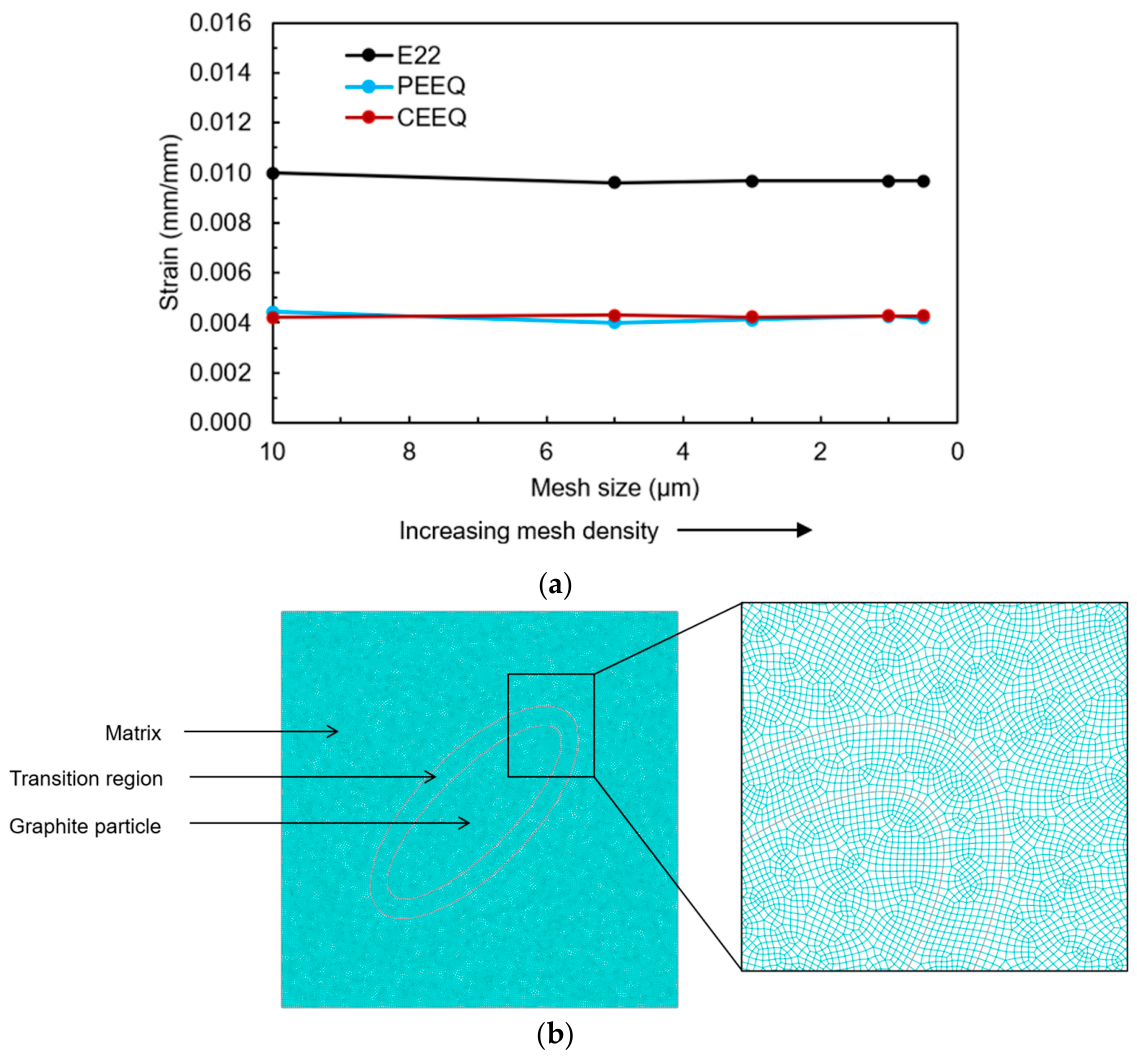
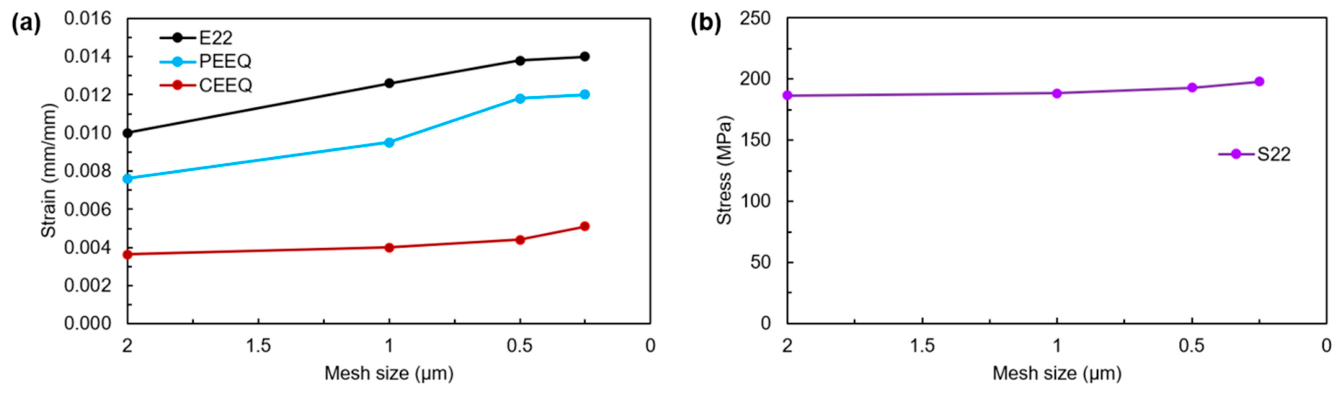
The numerical simulations were completed with 8-node quadratic 2D CPS8 plane stress finite elements. The 8-node elements can capture quadratic displacement and linear stress variation within the element. The 8-node plane stress finite elements were chosen to capture the local high stresses and stress redistributions around the graphite particles. Based on the mesh-sensitivity analysis (see its results in Figure 3a), a typical element size of about 0.5 microns was used in the full model for particles with idealised inclusion geometries. Details of the mesh size and results of the mesh sensitivity study for a realistic geometry of inclusions are covered in Section 4.5. An example of the mesh used in the simulations is shown in Figure 3b.
The default thickness for plane-stress analysis in Abaqus is a unit thickness. The plane-stress element formulation ensures that the out-of-plane stress, σ z , is zero irrespective of thickness defined in the analysis.
Figure 3. (a) Results of mesh-sensitivity study. (b) Example of mesh used in RVE model (total number of nodes: 149,043; total number of elements: 49,414).
Applsci 16 07894 g003

2.4. Geometry, Loads and Boundary Conditions for Simulations
The Abaqus model was set up with millimetre as unit of length and Newton as unit of force, while all the creep parameters were derived in an hour-based time scale. The 2D RVE used in the simulation had 100 μm × 100 μm dimension (Figure 4). Initially, the matrix-only configuration was analysed, so that the effect of graphite particles can be clearly quantified. The average graphite volume fraction for the material used in this research was 9.04%. The volume fraction was calculated from the microstructural analysis of the SEM images following standards [7,9,75]. To maintain the same graphite-to-matrix ratio, the 2D RVE models with inclusions were created with graphite particles covering 9.04% area fraction. The matrix-only model, the model with a circular graphite particle and the model with an elliptical graphite particle were developed (Figure 4).
The aspect ratio for the elliptical particles was set to 3.02 based on the microstructural analysis of the material. Further models were created to study the effects of orientation and aspect ratio of particles using models with elliptical inclusions; details of those models are covered in Section 4.3 and Section 4.4. Details of the models with realistic inclusions are covered in Section 4.5.
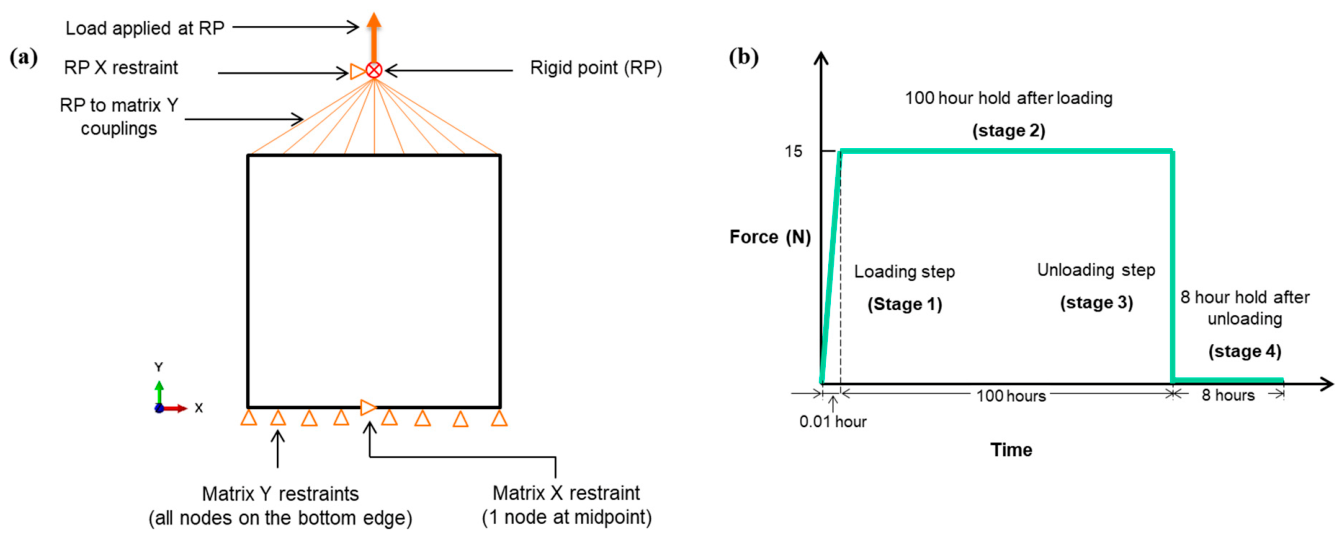
The boundary conditions used in the simulations are shown in Figure 5a. A rigid point was added above the top face of the matrix, and it was connected to the matrix using kinematic coupling in the Y direction. This setup ensured a uniform displacement at the top face under the applied load. The bottom face of the matrix was restrained in the Y direction to react to the load. The rigid point and the midpoint of the bottom face were restrained in the X direction to prevent the rigid-body motion. This boundary condition setup ensured symmetric material behaviour on the left and right faces and that the model was not over- or under-constrained.
A sensitivity study was conducted for the model with a circular graphite domain modelled as a solid by comparing results from these boundary conditions (results covered in Section 4.2) against a model with periodic boundary conditions created with EasyPBC plugin in Abaqus [76]. It was found that the difference in the maximum axial stress between these two cases was 3% for the purely elastic model, which, after stage 2, reduced to 0.3% in tension and 2.4% in compression in the viscoplastic model. This result demonstrated that the effect of boundary conditions on stresses is small.
Creep simulations were completed with mechanical load varying with time as presented in Figure 5b. The load was first ramped up from 0 to 15 N in 0.01 h (equivalent to 36 s) in stage 1. This load ramp-up represented the load increase in the creep tests. The maximum load of 15 N generates 150 MPa nominal stress in the matrix (this was verified with the model consisting only of elastic matrix). The load magnitude was the same in tension and compression cases, but the load direction was +Y for the former and -Y for the latter. The load was held constant for 100 h in stage 2 to represent 100 h creep tests reported in our previous study [25]. At the end of this step, the load was instantaneously reduced to zero (stage 3) followed by a hold period of 8 h (stage 4), which was added to monitor stress evolution after unloading.
All the steps in the analysis included the use of *VISCO option in Abaqus to simulate the time-dependent creep behaviour in the analysis. In the numerical simulations, the initial time increment for stage 1 was set to 1 × 10⁻⁶, 1 × 10⁻⁹ for stage 2, and 1 × 10⁻⁵ for stage 4. The creep strain error tolerance was set to 1 × 10⁻⁵ for all the stages. No other stabilisation or regularisation parameters were used in the simulations.
Figure 5. RVE model setup: (a) boundary conditions; (b) load-time history.
Applsci 16 07894 g005

2.5. Quantification of Creep Parameters and Simulation Methodology

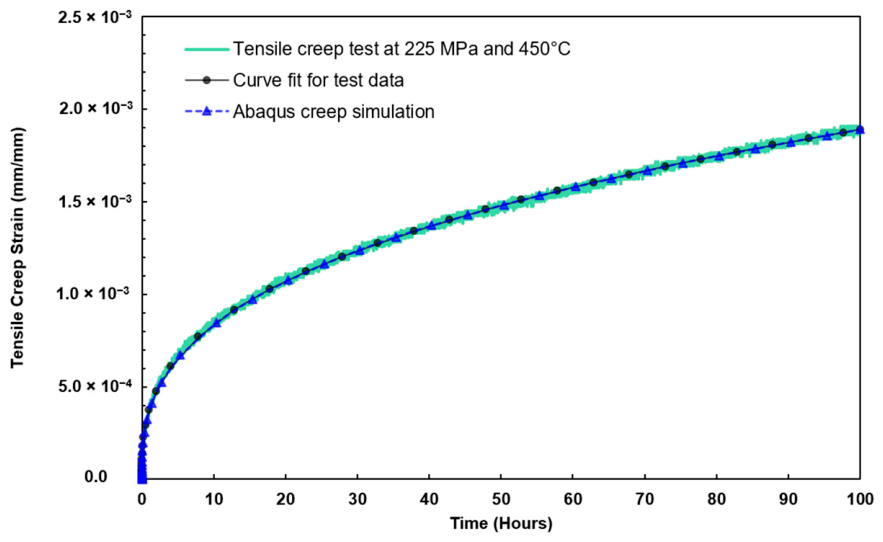
The process of derivation of creep parameters and their correct application in the Abaqus simulation was checked by using a matrix-only, constant-stress model. For this check, creep parameters of the matrix were derived from the tensile creep test at 225 MPa and 450 °C from our test data [25], employing Equations (5) and (6) as shown in Table 3.
A comparison of the creep strains from the test, the curve fit used for the experimental results, and the creep strains obtained from the Abaqus simulation are shown in Figure 6. A perfect match between the test results and the Abaqus simulation confirms the correct derivation of creep parameters and their use in the simulation. The result shows that the model can effectively capture the macroscopic creep behaviour of the material. This model was then extended to introduce the graphite particle to understand the localisation effects due to the inclusions in the matrix.
This paper includes multiple results with different particle shapes, as well as various approaches for modelling graphite and with matrix modelled as elastic, viscoelastic or viscoplastic. To simplify the review of results, their naming convention is given Table 4.

3. Results for Inclusions Modelled as Voids

This section presents the results for the analysis with particles simulated as circular voids with elastic, viscoelastic and viscoplastic matrix. Below, absolute magnitudes of tensile and compressive axial stresses are considered in graphs for comparability.

3.1. Effects of Plasticity and Viscosity After Stage 1

As mentioned previously, the first loading step in the analysis is 36 s (0.01 h) long and it represents a ramp-up of load in the creep test. Even though the load step time is rather small, the material can undergo both plasticity and viscosity in this short period of time. To quantify the effect of these mechanisms, simulations were conducted for this loading step, first with the elastic matrix, second with the viscoelastic matrix and lastly with the viscoplastic matrix.
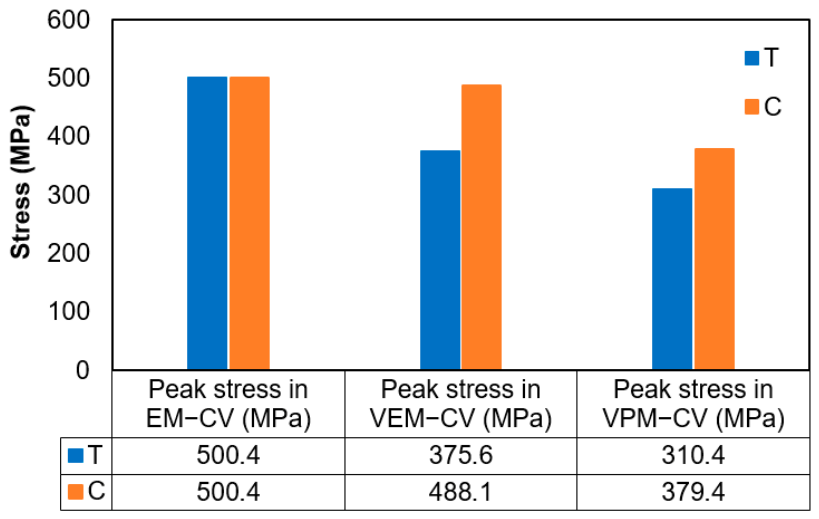
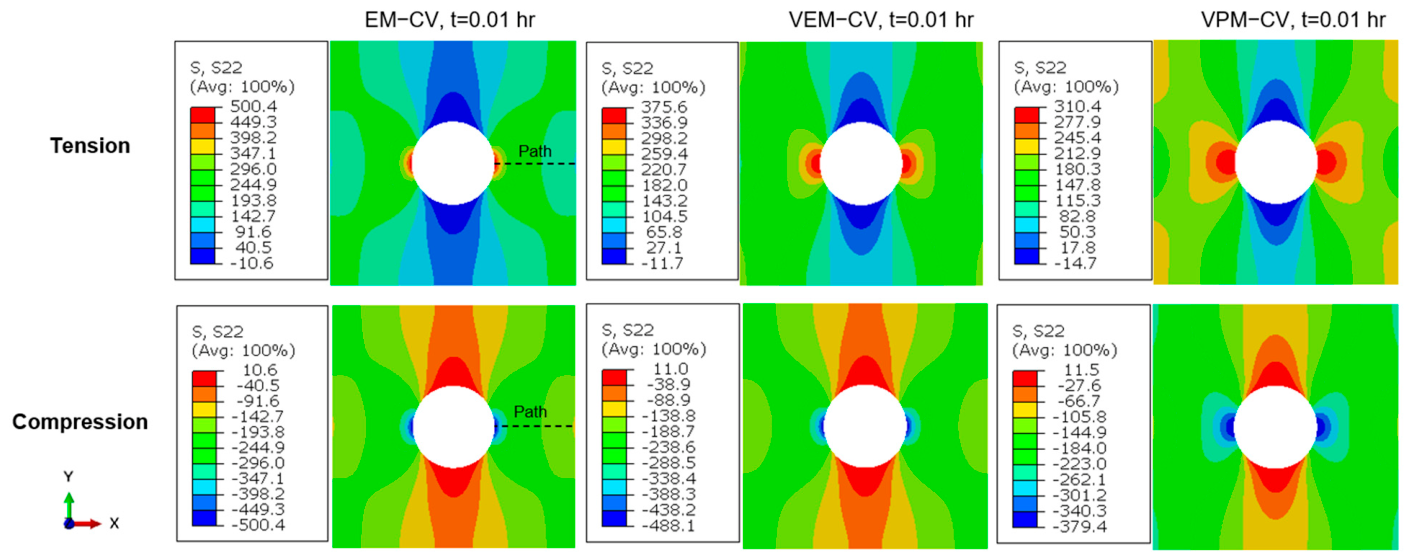
The distributions of axial stress obtained from these simulations are shown in Figure 7 and the summary of local peak stresses is given in Figure 8. Under the applied load of 150 MPa, the maximum stress of 500.4 MPa was generated in the elastic matrix. This peak stress represents a stress concentration factor of 3.3 caused by the presence of the void. As expected, the magnitude of peak elastic stress was the same under both tension and compression. In the viscoelastic model under tensile loading the peak stress at t = 0.01 h reduced to 375.6 MPa—about 25%—due to stress relaxation. On the other hand, this model under compressive loading showed the peak stress magnitude of 488.1 MPa, which was only a reduction of about 2.5%. In the viscoplastic model in tension, the peak stress dropped even more—to 310.4 MPa (38% reduction)—whereas under compression loading, it was 379.4 MPa (24% reduction). These results demonstrate that during the loading step, the effect of viscosity was much more dominant for tension compared to that in the compressive loading. This was because (a) the tensile creep rate was higher, resulting in higher stress relaxation and (b) the tension–compression asymmetry resulted in lower yield strength in tension compared to compression. Both these effects led to lower stresses in tensile loading condition.
Another particularly important observation is that even though the macroscopic stress was low (150 MPa), the local peak stresses were extremely high, even exceeding the material’s yield strength. Such material behaviour at the microstructural level can only be assessed with the micromechanical models, without which the local effects are likely to get ignored. It is highlighted that the use of homogenisation or averaging results over the RVE would not allow a correct assessment of the effects of local high levels of stress and strain concentration, which can be the main reason for microscopic damage (e.g., separation between the matrix and inclusion), crack initiation and loss of structural integrity.
Figure 7. Axial stresses for CV models at t = 0.01 h.
Applsci 16 07894 g007
Figure 8. Effect of plasticity and viscosity on magnitudes of axial stress at t = 0.01 h in CV models.
Applsci 16 07894 g008
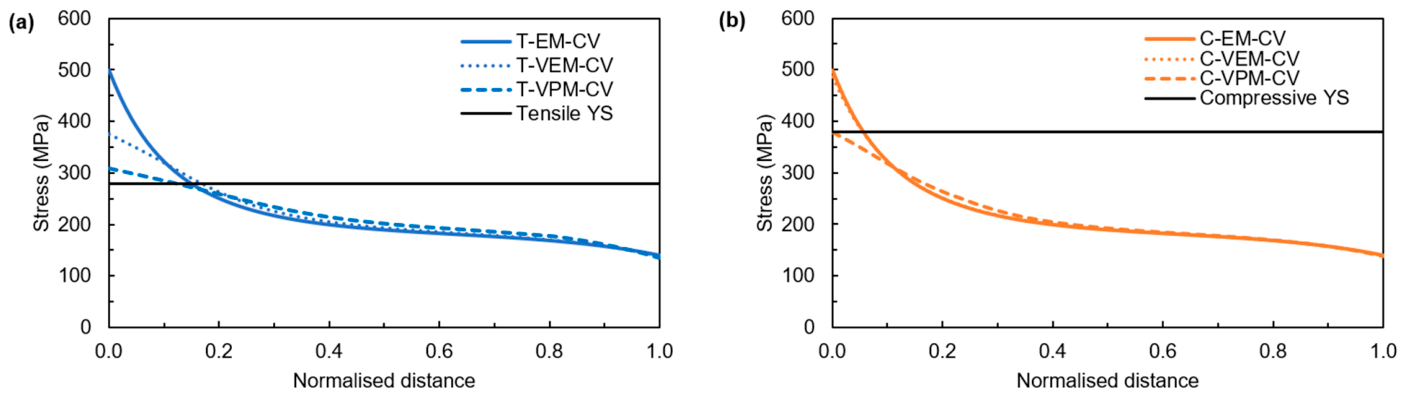
The contour plots in Figure 7 highlight the extent of stress redistribution in the matrix due to viscosity. The stress redistribution along the paths marked in Figure 7 are presented in Figure 9 for direct comparison. Apparently, the maximum stress relaxation occurs around the peak stress (Figure 9a), with stress magnitudes diminishing close to the yield stress. Under tensile loading, the effect of stress redistribution caused by plasticity and viscosity was observed for almost 90% of the path. In contrast, in case of compression loading, the stress redistribution due to viscosity was almost negligible, but significant stress redistribution could be seen when both creep and plasticity were introduced into the model. The overall effect on the stress distribution under compressive loading is visible for some 40–50% of the path. It is noted that this level of stress redistribution occurs only within 36 s; so, a much higher level of stress redistribution can be expected during the full 100 h creep hold stage (stage 2).

3.2. Effects of Creep and Plasticity After Stage 2

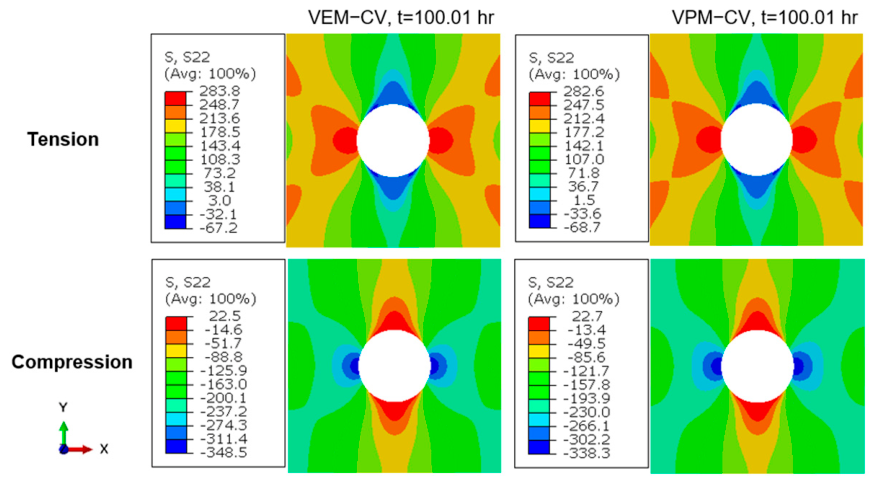
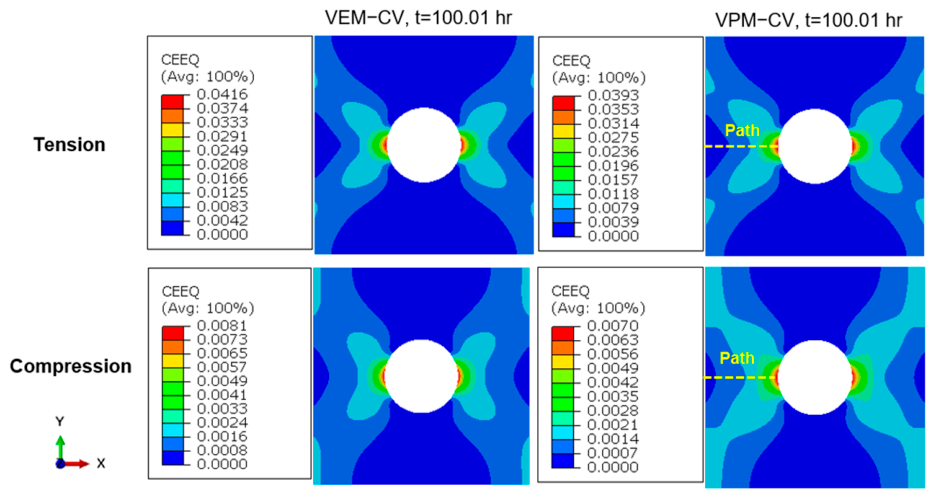
The axial stresses and the creep strains for the viscoelastic and viscoplastic models with circular voids after stage 2, i.e., at t = 100.01 h, are shown in Figure 10 and Figure 11, respectively.
Multiple observations can be made based on these results:
  • For tensile loading, the peak stresses after stage 2 are similar for viscoelastic and viscoplastic models. In both cases, the stresses relaxed close to the tensile yield stress. This suggests that stresses above the yield point were redistributed because of the stress relaxation due to viscosity. The effect of plasticity was much higher in stage 1, whereas the effect of creep accumulated during the hold stage.
  • Under compressive loading, at the end of stage 2 the stresses relaxed close to 348 MPa with the viscoelastic matrix and to 338 MPa with the viscoplastic one. The relaxed local stresses were higher under compressive loading because of the lower creep (thus, lower stress relaxation) and due to the tension–compression asymmetry in the yield stress.
  • Viscous strains were lower in the viscoplastic model compared to the viscoelastic one. This was expected since the introduction of plasticity reduced the level of stresses which, in turn, reduced the creep strain. It is also noted that the predicted creep strains in compression were almost 80% lower than those in tension as expected due to lower levels of creep in compression.
  • The maximum local creep strain under tensile loading was close to 4% for both the viscoelastic and viscoplastic matrix. These strain levels are high compared to the approx. 1% strain at failure from the true-stress–strain curve shown in Figure 2a. It is noted that the creep test at 150 MPa stress at 500 °C did not show any signs of cracking or rupture at the end of the 100 h long creep test. These findings suggest that modelling of graphite particles as voids can overpredict the creep strains.
  • There is an important conclusion from this study applicable to creep analysis of any structures with stress concentrators. The results summarised in Table 5 show comparison of stresses and strains from the viscoplastic models with inclusions as voids against matrix-only simulations. The results show that with a stress concentration factor of 2.07 under tensile loading, the maximum local creep strain produced in the model could be about 53 times higher. Under compression loading a stress concentration factor of 2.53 resulted in maximum creep strain being about 14 times higher. These results highlight the effect of local stress concentration features on the creep strains produced in the material: relatively small local stress increases can lead to a significant growth in creep strains over a period of time that can potentially lead to the onset of creep-related failure mechanisms in the product.

4. Results for Models with Solid Inclusions

This section covers the results of analyses completed with graphite particles modelled as isotropic solids. In all these cases, the matrix was modelled with viscoplastic properties.

4.1. Comparison of Results with Different Inclusion Modelling Approaches

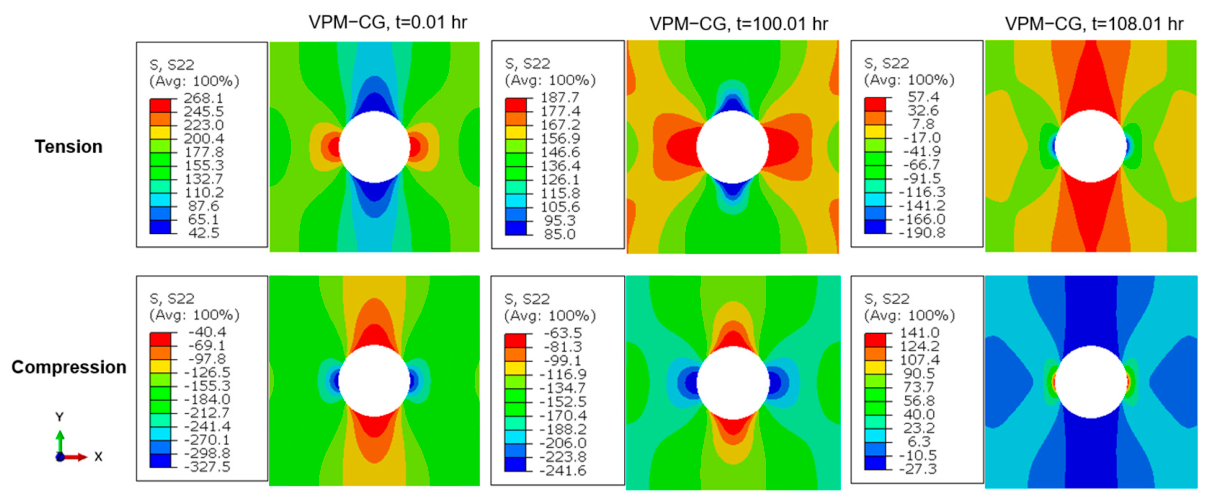
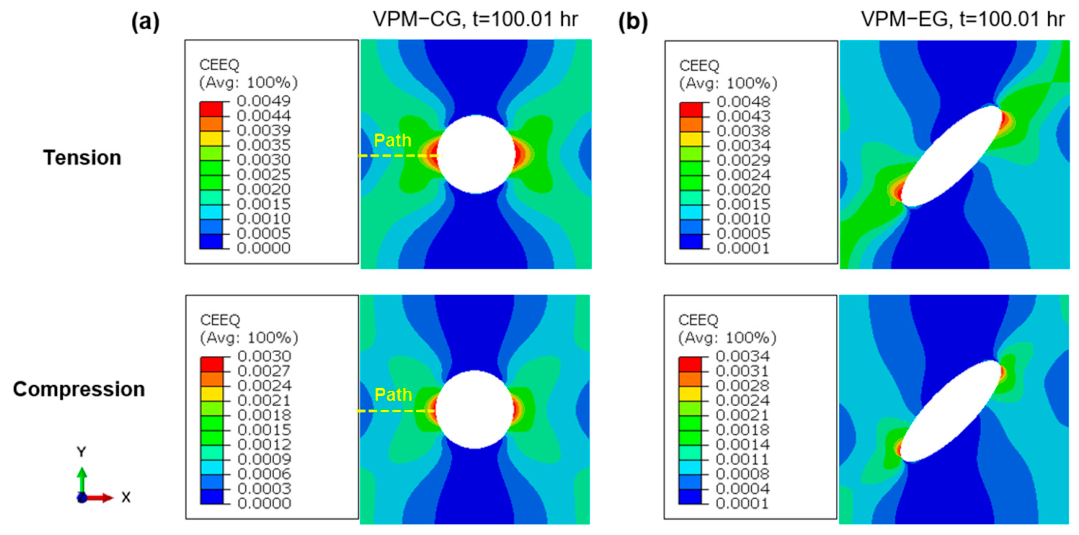
Comparison of stresses and creep strains with different graphite modelling approaches for circular inclusion in the viscoplastic matrix is given in Table 6. The main results for stresses and strains are presented in Figure 12, Figure 13, Figure 14 and Figure 15. The stress distributions for the matrix with the solid circular graphite particle after stages 1 and 2 are shown in Figure 13, while those for creep strain after stage 2 are in Figure 15a.
The following observations can be made based on these results:
  • Modelling the graphite particles as isotropic solids reduced the stresses and creep strains in the matrix for both tensile and compressive loading. At the end of stage 2, stress reduced by about 34% under tensile loading and by about 29% in compression. The resultant creep strain after stage 2 under tensile loading was 0.49%—down from 3.93% obtained with inclusions modelled as voids.
  • Stress relaxation and redistribution due to viscosity was evident in both modelling approaches during the 100 h creep period. However, the stress relaxation was more pronounced in the model with solid graphite even though the peak stress was higher in the void model. This behaviour can be explained with reference to Figure 12, which shows distributions of the normalised creep strains on the paths marked in Figure 11 and Figure 15a. In the void model, the creep strain dropped rapidly away from the peak-stress location, but in the solid graphite model, the distribution of creep strain was more gradual, leading to higher stresses over a larger region. This behaviour was enabled by the solid graphite particle that affected the spread of creep deformation over a larger region. The difference in the extent of creep strain distribution is evident upon closer inspection of Figure 11 and Figure 15a.
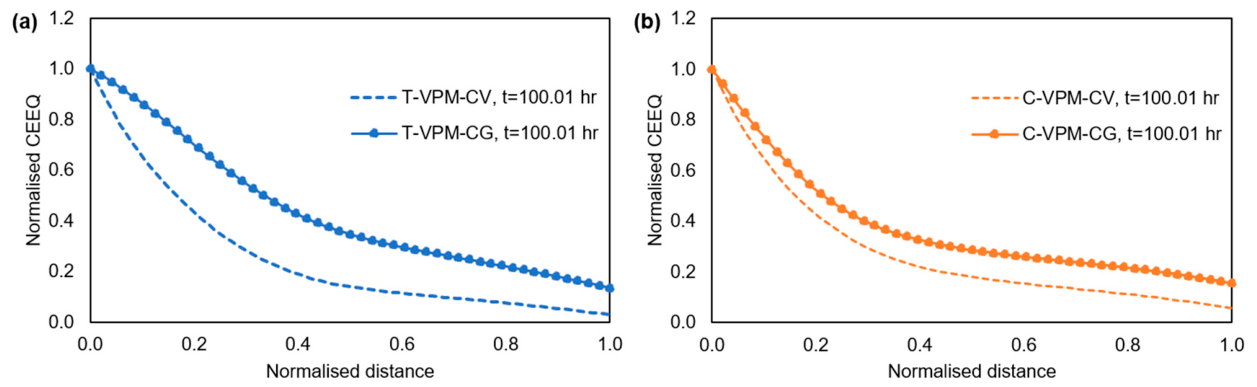
Figure 12. Normalised creep strains along paths in Figure 11 at t = 100.01 h: (a) tensile loading; (b) compressive loading.
Applsci 16 07894 g012
  • The residual stresses at the end of stage 4 as shown in Figure 7 and Figure 13 were caused by the spring-back effect. The local residual stresses were of opposite type compared to the loading, i.e., compressive residual stresses were generated under tensile loading and vice versa.
Figure 13. Axial stresses for circular solid graphite particle.
Applsci 16 07894 g013

4.2. Effect of Inclusion Shape

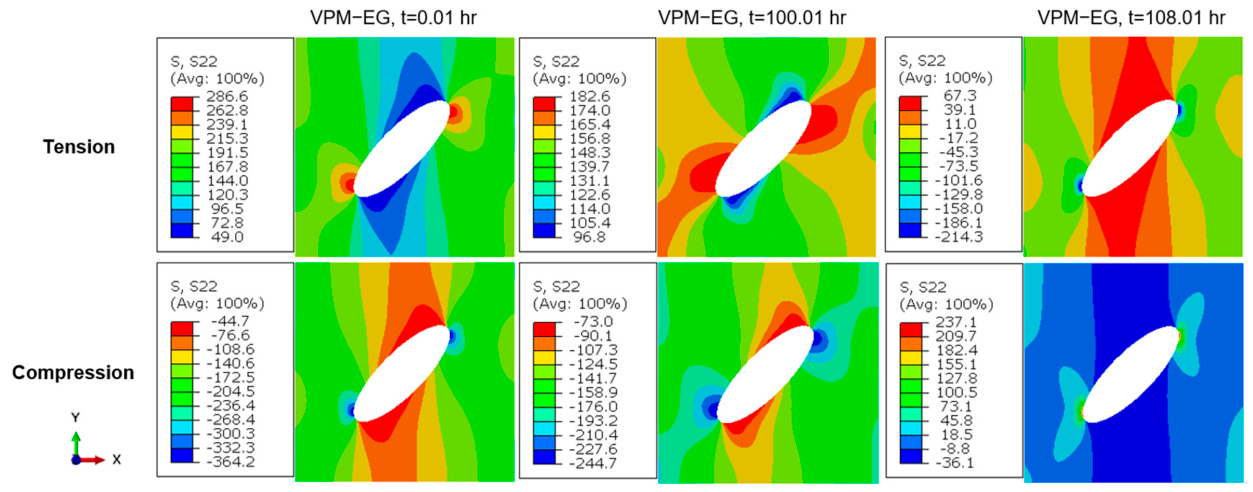
To understand the effect of the shape of graphite particles on creep response of the material, RVE models were created with circular and elliptical particles (Figure 4). Graphite was modelled as an isotropic solid for these cases with material data provided in Section 2.2. The stress plots for both graphite shapes under tensile and compressive loading regimes are shown in Figure 13 and Figure 14, respectively, while the distribution of creep strains for these cases are given in Figure 15.
Figure 14. Axial stresses for elliptical solid graphite particle.
Applsci 16 07894 g014
Several observations can be made based on the obtained results:
  • Comparison of distributions of stresses and creep strains for these two particle geometries demonstrated a big impact of the shape of inclusions. This highlights the possible impact of multiple particles of different geometries on the creep progression in the matrix.
  • As expected, the elliptical particles caused higher stress concentration. This led to higher stresses after stage 1 under both tension and compression. However, after stage 2, the impact of stress concentration diminished, and the stresses relaxed to similar levels for both circular and elliptical particles.
  • The creep strain distributions show some interesting results. Under tensile loading, the maximum creep strain was higher for the circular graphite particle. This observation is striking since the peak stress at the start of stage 2 was higher for the elliptical inclusion. It appears that the higher initial stress led to higher initial creep that caused higher stress relaxation and more pronounced stress redistribution, eventually leading to a lower maximum creep strain after stage 2. On the other hand, the level of creep under compression was lower, so the accompanied stress relaxation was also lower. The net effect is that under compression, the creep strains were higher for elliptical particles compared to circular ones. This observation is in line with previous results that the overall magnitude of compressive creep was lower and the effect of tension–compression asymmetry in the yield stress further reduced the effect of stress relaxation and stress redistribution under compressive loading.
Figure 15. Creep strains after stage 2 for different particle shapes: (a) circular; (b) elliptical.
Applsci 16 07894 g015
  • As observed previously, generally the stress levels were higher under compressive loading.
  • After stage 4, the effect of stress concentration caused higher residual stress in the case of an elliptical particle compared to the circular one.
Additional analysis was conducted to study the effects of using 2D plane-stress and plane-strain models with different graphite particles. The results for matrix creep strain obtained at the end of stage 2 from this study are shown in Table 7. The results showed that the plane-strain models consistently produced lower strains compared to the plane-stress ones due to the inherent constraint in the former ( ε z = 0 ) . However, both models followed similar trends with creep strain being lowest for the matrix-only model followed by the models with circular and elliptical inclusions. As both modelling approaches show similar trends, plane-stress models were used for all other studies reported in the paper.

4.3. Effects of Inclusion Orientation

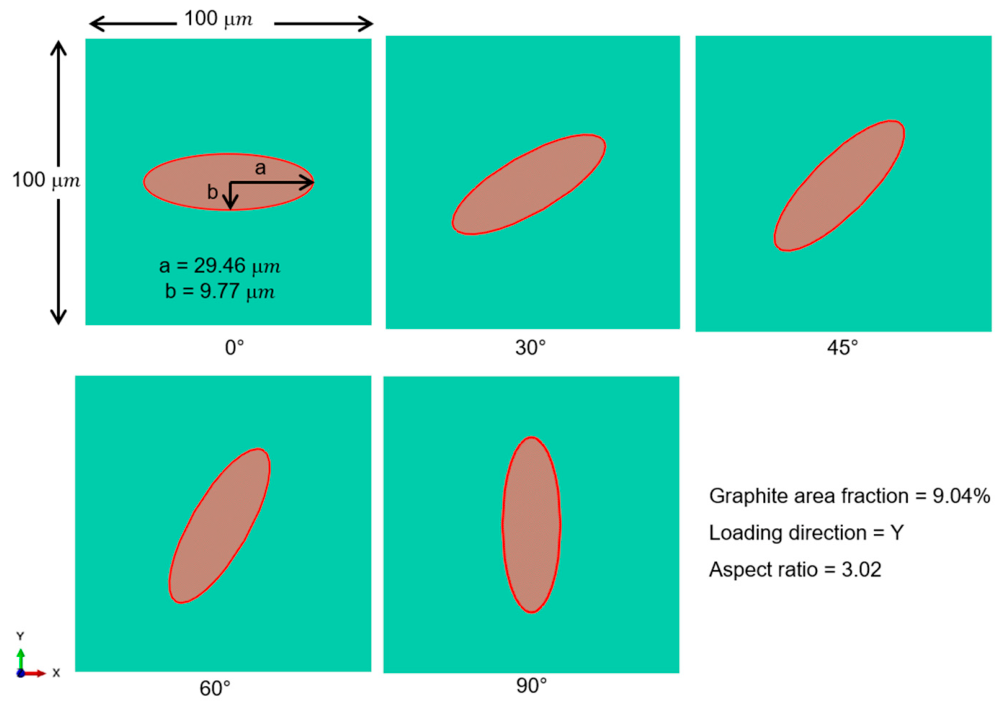
The microstructure of CGI (Figure 1) clearly demonstrates the randomness in the orientation of graphite particles. The effect of this orientation on creep response of CGI is investigated in this section. This analysis is similar to the study reported in the literature [26] but with inclusion of time-dependent behaviour under tensile and compressive loading. For this study, the elliptical graphite particle model from Figure 4c was updated to orient the graphite particles at 0°, 30°, 45°, 60° and 90° to the X axis (Figure 16). Only the orientation of inclusions was changed in these models without changing their aspect ratio and area fraction. The meshing approach, load steps and loading and boundary conditions remained unchanged. These simulations were completed with the viscoplastic matrix and solid isotropic graphite particles.
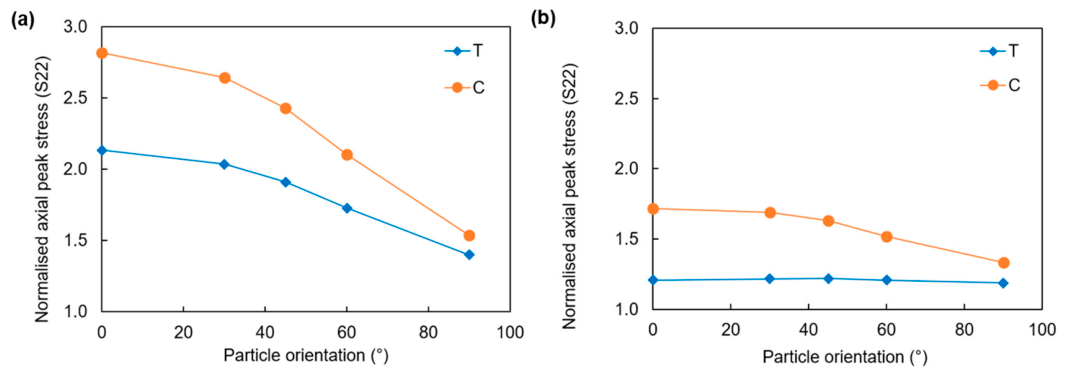
To simplify the comparison of simulation results, the peak stress S22 in each model was normalised with the nominal stress of ±150 MPa from the matrix-only model, (+ve stress for tension and -ve stress for compression). The normalised stress gives an indication of stress concentration effect for each model. The normalised axial stress was calculated after stages 1 and 2 for each particle orientation. These results are shown in Figure 17. The following observation can be made based on the results:
  • The peak stress after stage 1 is a function of particle orientation, with the 0° particle generating the maximum stress and the 90° particle generating the minimum stress. This declining trend was observed for both loading regimes, with peak stresses in compression generally being higher.
  • After stage 2, under tensile loading, the stress relaxed to roughly the same level for all orientations. However, under compressive loading, stresses for the 0° particle were highest, reducing progressively with the increase in the orientation angle. Overall, the stresses in compression were higher as they were in the previous results.
Figure 17. Effect of particle orientation on normalised axial peak stress (S22): (a) after stage 1; (b) after stage 2.
Applsci 16 07894 g017
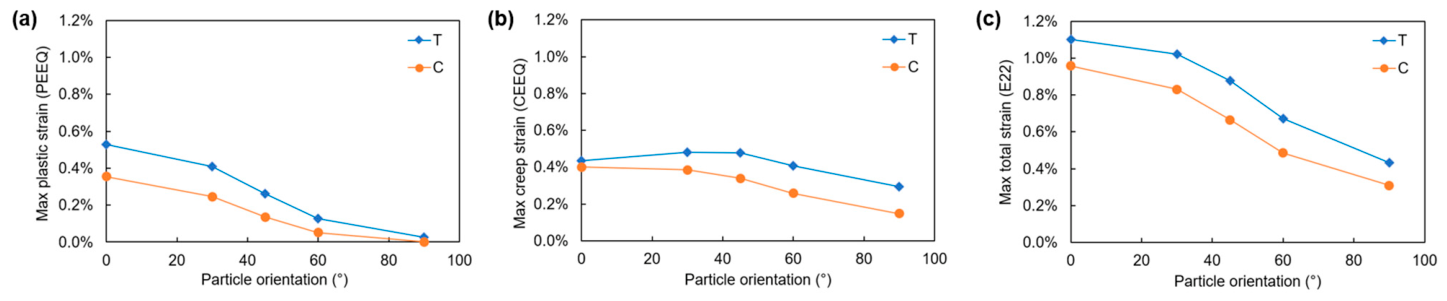
For each orientation of graphite particles, the magnitudes of maximum equivalent plastic strain (PEEQ), maximum equivalent creep strain (CEEQ) and maximum total strain (E22) were extracted after stage 2 (Figure 18). All these reported strains are true strain output from Abaqus. It is noted that the graphs show the overall maximum of each strain distribution and that the location of each peak strain may thus differ. The idea is to show the effects of plasticity and viscosity for each analysed particle orientation.
The following observation can be made based on these results:
  • The effect of particle orientation on maximum plastic strain follows the decreasing trend observed for stresses. The plastic strain was higher for tensile loading; for both cases it decreased with the growth in the orientation angle.
  • In contrast, for tensile loading, the creep strain initially slightly increased with orientation, subsequently diminishing for orientations above 45°. For compressive loading, the evolution of maximum creep strain with orientation followed that for stresses continuously reducing with increasing angle.
  • The total strain is the combination of elastic, plastic and creep strains, and it reduced with the particle orientation from 0° to 90° following the maximum stress distribution. Continuing the observations made throughout this study, the tensile plastic, creep and total strains were higher compared to their compressive counterparts.
  • Based on the results, it was found that elliptical graphite particles aligned along or close to the loading direction resulted in the lowest stress-concentration effect, lowest creep and plastic strains and, overall, provided the best performance of CGI under the applied loading conditions.
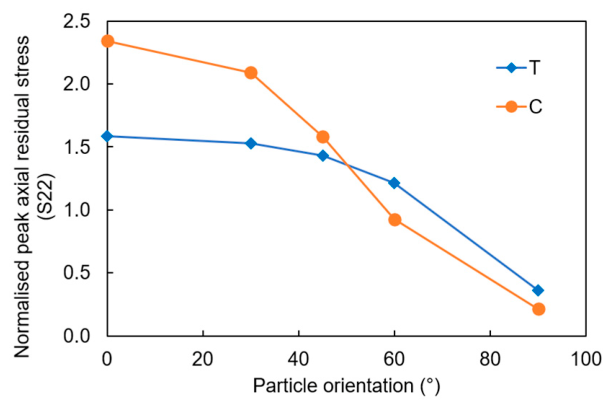
As seen in previous results, the permanent deformations due to macroscopic creep and plasticity led to the generation of residual stresses. The highest magnitudes of these residual stresses were compressive in the case of tensile loading and vice versa because of the spring-back of the material upon unloading. The normalised peak axial residual stresses (peak axial residual stresses normalised by 150 MPa) after stage 4 for models with different particle orientations are shown in Figure 19. It is noted that these stresses clearly depend on the particle orientation, which defined the peak stress and, consequently, evolution of creep and plasticity around the graphite particles. Some interesting observations can be made based on these results:
  • In the range of particle orientation between 0° and 45° the level of residual stresses in compressive loading was higher. This was caused by much higher levels of stress redistribution due to creep and plasticity under tensile loading, so the effect of spring-back was less prominent in tension. As observed before, the level of creep and plasticity was lower under compression, resulting in a more dominant effect of spring-back after unloading.
  • For particle orientations between 45° and 90°, it was noted that the stress concentration effect was much lower and, hence, showed diminished levels of creep and plasticity. Additionally, creep and plasticity effects were lower under compression. As a result, (a) the residual stresses were generally lower and (b) residual stresses in compression were lower than those in tension.
Figure 19. Effect of particle orientation on normalised peak axial residual stresses (S22).
Applsci 16 07894 g019

4.4. Effects of Aspect Ratio of Inclusions

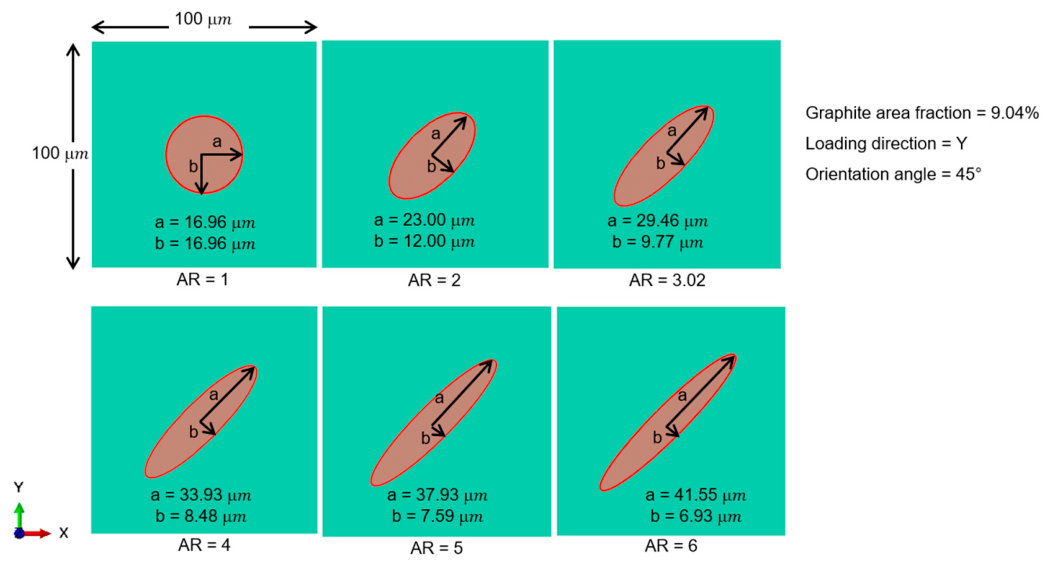
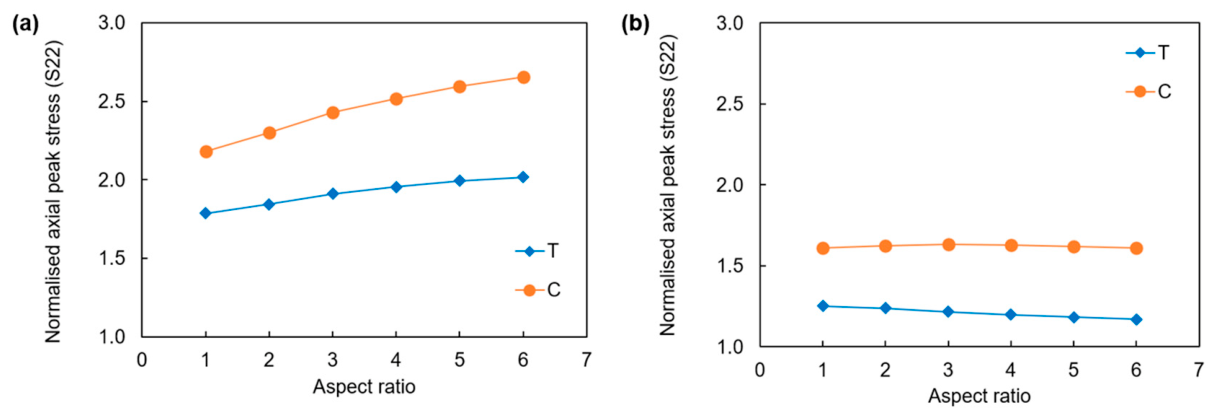
The microstructure of CGI material exhibits a wide range of aspect ratios of graphite inclusions (Figure 1). This section presents results of the numerical analysis to understand the effect of aspect ratio (AR) on the creep response CGI. The RVE models with elliptical graphite particle with AR values from 1 to 6 were used for this analysis (Figure 20). As before, the graphite area fraction was kept at 9.04% but the major and minor diameter of the elliptical particles were modified in each model to obtain the required aspect ratio. The meshing approach, loading steps, load and boundary conditions remained the same as in previous analysis. These simulations were completed with the viscoplastic matrix and solid isotropic graphite particles.
It is noted that the change in the aspect ratio of particles affected the distance between the particles and the external boundaries, so the obtained results also had a contribution from this effect.
Figure 20. RVE models to study effect of aspect ratio.
Applsci 16 07894 g020
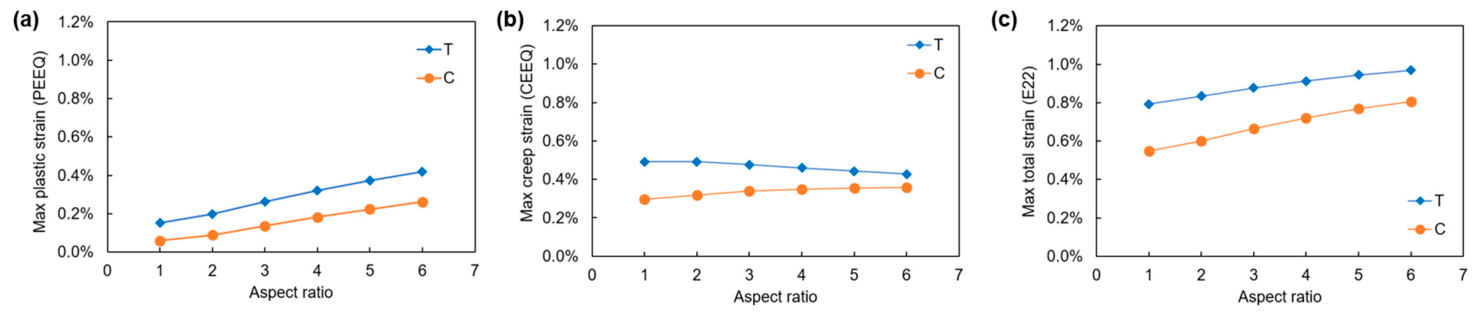
The obtained simulation results demonstrated the effect of particle shape on both stresses and strains in CGI (Figure 21 and Figure 22). The following observations can be made based on these results:
  • As expected, the peak stresses in the material after initial loading in stage 1 exhibited an increasing trend with growing AR for both tensile and compressive load cases. After long-term creep (stage 2), stresses relaxed to similar levels for all the studied aspect ratios. Also, as before, the stress levels under compressive loading were consistently higher.
  • The maximum plastic strain increased almost linearly with aspect ratio as expected due to the increase in the stress levels. It is interesting to note that the maximum creep strains were not highly affected by the aspect ratio. This can be explained by the effects of stress relaxation due to creep as also found in previous models.
Figure 21. Effect of aspect ratio of particles on normalised peak axial stress (S22): (a) after stage 1; (b) after stage 2.
Applsci 16 07894 g021
Figure 22. Effect of aspect ratio of particles on strains after stage 2: (a) maximum plastic strain (PEEQ); (b) maximum creep strain (CEEQ); (c) maximum total strain (E22).
Applsci 16 07894 g022
  • The total strain showed an increasing trend with AR mainly due to the increase in plastic strains. In line with the observations made throughout this paper, the plastic, creep and total strains were higher under tensile loading. Based on the total-strain results, lower aspect ratios are preferrable from the structural integrity perspective. It is noted that the CGI specifications do not allow more than 20% nodular particles, and some of the important characteristics of this cast iron are due to its microstructure. So, this parameter should be specially considered for optimum performance under high-temperature applications.
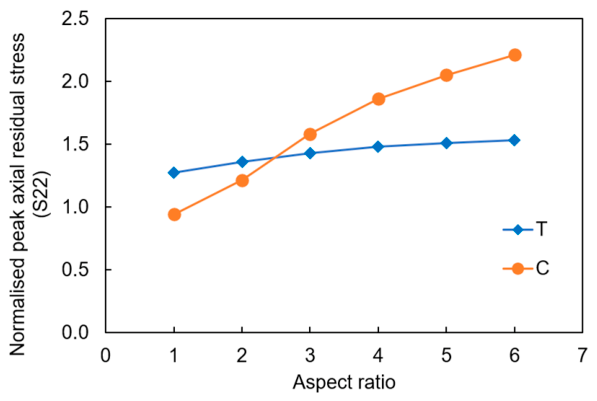
The normalised peak axial residual stresses (peak axial residual stresses normalised by 150 MPa) after stage 4 demonstrate different sensitivity to the aspect ratios (Figure 23). Generally, the effect of AR for tension was rather small, while for compression, an increasing trend was obvious. For AR ≥ 3 the level of residual stresses in compressive loading was higher. This was a result of a much higher level of stress redistribution due to creep and plasticity under tensile loading, so the effect of spring-back after unloading was less prominent in tension. For graphite particles with AR = 1 and 2, the stress-concentration effect was much lower, and, hence, the influence of creep and plasticity was less pronounced. As a result of this, the residual stresses were generally much lower in compression.

4.5. Effects of Realistic Geometry of Inclusions

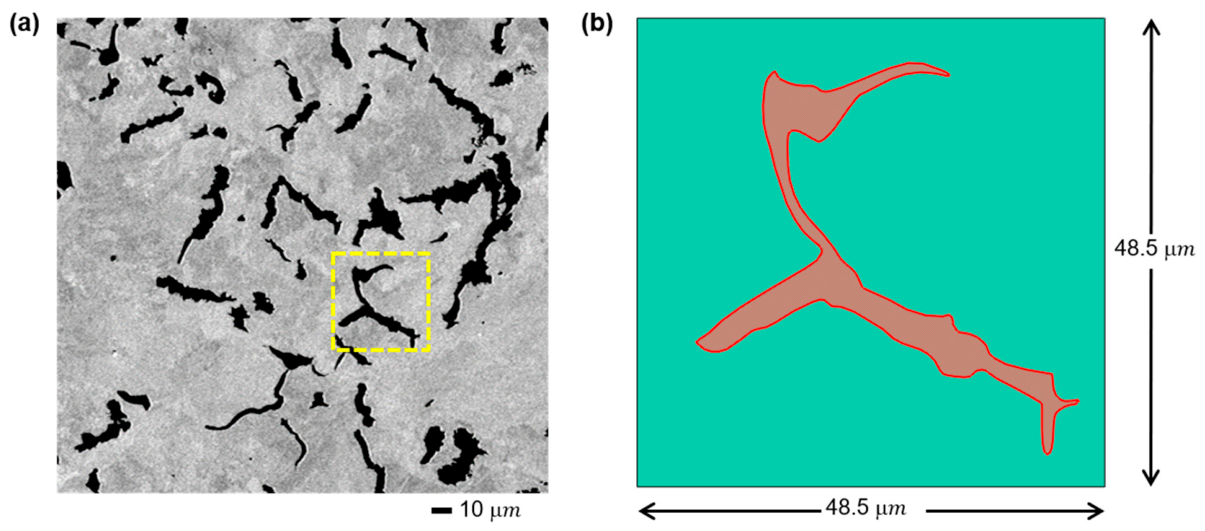
All the results shown so far were obtained using idealised inclusion geometries that differed substantially from the actual shapes of graphite particles. To understand how this simplification affects the results, analysis was completed with inclusion geometry taken directly from SEM images as shown in Figure 24a. Geometry of the selected inclusion was more complex compared to the typical vermicular inclusions found in CGI but was specifically chosen for the diversity of its features, e.g., a long vermicular region, a branch feature and notch-like endings. The size of the matrix region (Figure 24b) was adjusted to maintain the same area fraction of graphite as in previous studies—9.04%.
A mesh-convergence study was also implemented for the model with realistic inclusion geometry due to the presence of finer features. Results from this study at location A identified in Figure 25 are shown in Figure 26 after stage 2. They showed a converging trend in stresses and strains and, thus, the smallest element size of 0.25 micron was used in the numerical simulations.
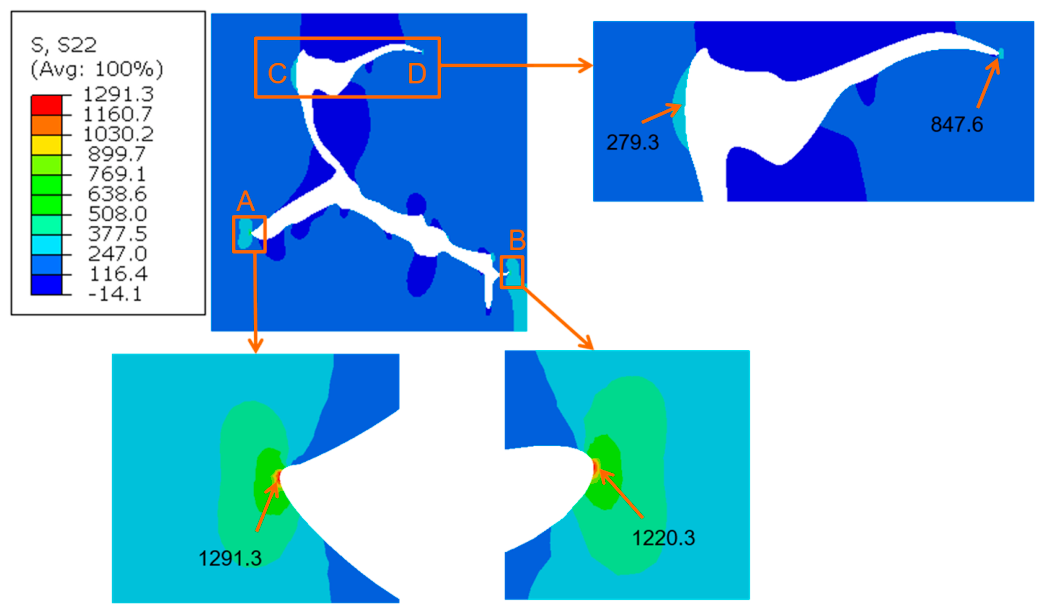
The loading steps, load and boundary conditions were unchanged from the previous analyses. This simulation was completed with inclusion modelled as a solid isotropic particle. Stresses from the elastic analysis at the end of stage 1 are shown in Figure 25, while those at key locations from the viscoplastic analysis are given in Table 8. The creep strains from the viscoplastic analysis are presented in Figure 27.
Figure 24. (a) SEM image highlighting the graphite particle chosen for analysis; (b) RVE model with realistic particle.
Applsci 16 07894 g024
Figure 25. Elastic axial stresses in model with realistic particle at the end of stage 1.
Applsci 16 07894 g025
Figure 26. Results from mesh-sensitivity study at location A: (a) strains; (b) stress.
Applsci 16 07894 g026
The following observations can be made based on these results:
  • As expected, the stress-concentration features of the realistic particle developed localised high stresses with peak stresses exceeding the material’s yield strength by a factor of over 4 (Figure 25). However, accounting for creep and plasticity, these local high stresses relaxed significantly, initially in the loading step and later through stage 2—see Table 8.
  • Comparison of maximum plastic, creep and total strains after stage 2 with different inclusion models is shown in Table 9. It was observed that creep strains in the realistic particle model were similar to those obtained with the idealised geometries. However, the notch-like features of the realistic particle led to high plastic strains. This observation is in line with the findings from the aspect-ratio studies, which demonstrated an increase in plastic strain with the growing aspect ratio.
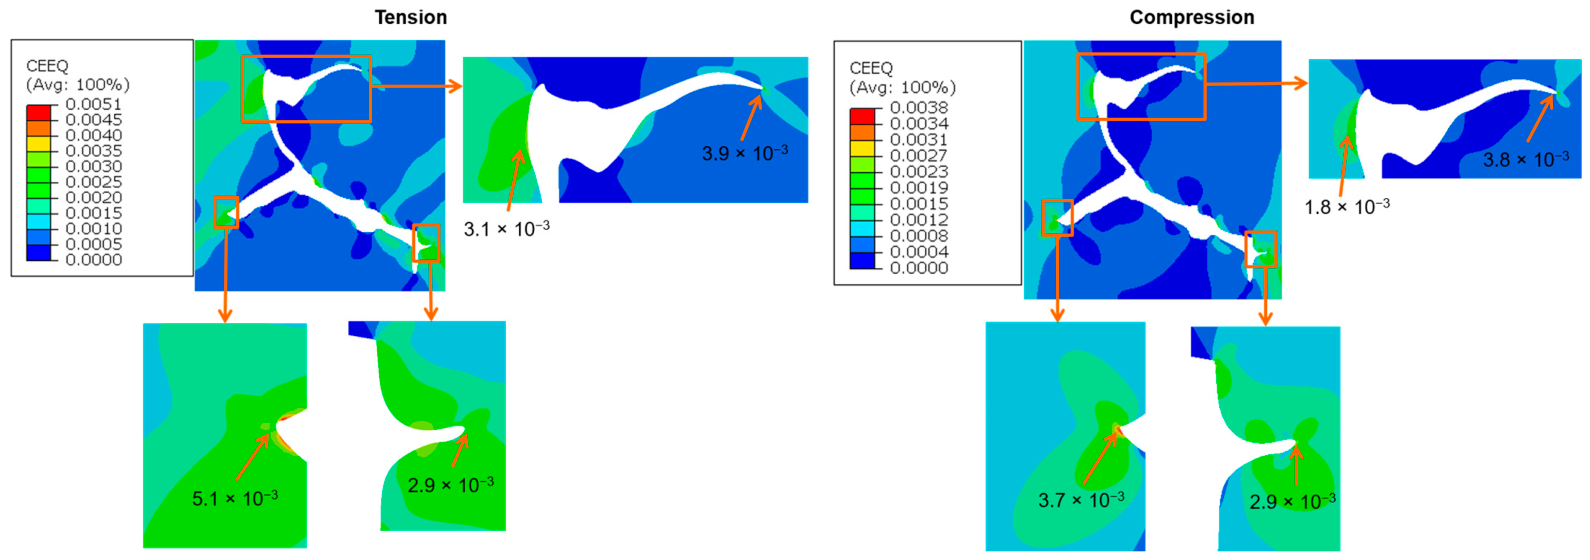
Figure 27. Creep strains after stage 2 for model with realistic particle.
Applsci 16 07894 g027
  • Based on these results, it can be beneficial to reduce sharp notch-like features in CGI material to reduce the localised high plastic strains in the material, which can drive premature failures.

5. Conclusions

The paper builds upon the results of our experimental work [25] and presents a detailed methodology for rigorous evaluation of creep at microscale in cast irons using 2D micromechanical models. The effects of elastic, viscoelastic and viscoplastic modelling of matrix were assessed. The study included the analysis of the effect of graphite morphology on creep deformation for circular and elliptical graphite particles; different orientations and aspect ratios were considered. All these studies highlight the influence of modelling approaches on the creep and plasticity behaviour of CGI and demonstrate the challenges and opportunities in the generation of realistic micromechanical models for such materials.
The key conclusions based on the analysis reported in this paper are summarised below.
Overall, the obtained research results highlight significant asymmetry in tension and compression in the material’s creep response. The differences between these two loading regimes were evident in all the studies, with higher effects of creep and plasticity in tension compared to compression. More detailed conclusions are as follows:
  • The micromechanical models showed that high local stresses were formed around the graphite particles even at relatively low macroscopic stresses. Such local stresses can exceed the material’s yield strength resulting in local plasticity and significant increase in creep strains over a long period of time.
  • The use of homogenisation or averaging results over the RVE would not allow a correct assessment of the effects of local high levels of stress and strain concentration, which can be the main reason for microscopic damage (e.g., separation between the matrix and inclusion), crack initiation and loss of structural integrity.
  • The qualitative trends from particle-orientation studies showed that elliptical graphite particles aligned along (or close to) the loading direction resulted in the lowest stress-concentration effect, lowest creep and plastic strains and, overall, provided the best performance of CGI under the applied loading conditions.
  • Similarly, the qualitative trends from the studies of aspect ratio and a complex realistic inclusion showed that inclusions with high aspect ratios and notch-like features increased the maximum plastic strain, but did not have a big impact on the maximum creep strain. Thus, having particles with low aspect ratios and rounded edges can be beneficial for optimum performance of cast irons in high-temperature applications.
  • Generally, idealised geometries of graphite inclusions provide a close approximation of stresses and strains in the material and representative idealised geometries may be used to speed up the analysis, especially in cases of parametric studies.

6. Outlook

The authors plan to expand this research to assess the effects of higher stress levels, the influence of the graphite and matrix interface (including evolution of debonding), and to get a better understanding of creep and plasticity in CGI using 3D simulations.

Author Contributions

Conceptualization, A.J., K.P.B. and V.V.S.; methodology, A.J., K.P.B. and V.V.S.; software, A.J.; validation, A.J.; formal analysis, A.J., K.P.B. and V.V.S.; investigation, A.J.; resources, A.J.; data curation, A.J.; writing—original draft preparation, A.J.; writing—review and editing, K.P.B. and V.V.S.; supervision, K.P.B. and V.V.S. All authors have read and agreed to the published version of the manuscript.

Funding

This research received no external funding.

Data Availability Statement

All data are available from the corresponding author upon request.

Conflicts of Interest

The authors declare no conflicts of interest.

References

  1. Stefanescu, D.M. (Ed.) Mechanical properties of compacted graphite iron. In Cast Iron Science and Technology; ASM International: Materials Park, OH, USA, 2017; pp. 472–480. [Google Scholar] [CrossRef] [Scilit]
  2. Stefanescu, D.M. Classification and basic metallurgy of cast iron. In Cast Iron Science and Technology; ASM International: Materials Park, OH, USA, 2015. [Google Scholar] [CrossRef]
  3. Berns, H.; Theisen, W. Ferrous Materials; Springer: Berlin/Heidelberg, Germany, 2008. [Google Scholar] [CrossRef] [Scilit]
  4. Ghodrat, S. Thermo-Mechanical Fatigue of Compacted Graphite Iron in Diesel Engine Components. Ph.D. Thesis, Delft University of Technology, Delft, The Netherlands, 2013. [Google Scholar] [CrossRef] [Scilit]
  5. Sirtuli, L.J.; Bello Bermejo, J.M.; Windmark, C.; Norgren, S.; Ståhl, J.E.; Boing, D. Machining of compacted graphite iron: A review. J. Mater. Process. Technol. 2024, 332, 118553. [Google Scholar] [CrossRef] [Scilit]
  6. ASTM A842-11a; Standard Specification for Compacted Graphite Iron Castings. ASTM International: West Conshohocken, PA USA, 2018. [CrossRef] [Scilit]
  7. ISO 16112:2017(E); Compacted (Vermicular) Graphite Cast Irons—Classification. International Organization for Standardization: Geneva, Switzerland, 2017. Available online: https://www.iso.org (accessed on 25 June 2026).
  8. J1887_201802; Automotive Compacted Graphite Iron Castings. SAE International: Warrendale, PA, USA, 2018. [CrossRef] [Scilit] [PubMed]
  9. BS EN 16079:2011; Founding—Compacted (Vermicular) Graphite Cast Irons. British Standard: London, UK, 2011. Available online: https://bsol.bsigroup.com/ (accessed on 25 June 2026).
  10. Megel, M.; Westmoreland, B.; Jones, G.; Phillips, F.; Eberle, D.; Tussing, M.; Yeomans, N. Development of a structurally optimized heavy duty diesel cylinder head design capable of 250 bar peak cylinder pressure operation. SAE Int. J. Engines 2011, 4, 2736–2755. [Google Scholar] [CrossRef] [Scilit]
  11. Pierce, D.; Haynes, A.; Hughes, J.; Graves, R.; Maziasz, P.; Muralidharan, G.; Shyam, A.; Wang, B.; England, R.; Daniel, C. High temperature materials for heavy duty diesel engines: Historical and future trends. Prog. Mater. Sci. 2019, 103, 109–179. [Google Scholar] [CrossRef] [Scilit]
  12. Mills, Z.G.; Finney, C.E.A.; Haynes, J.A.; Trofimov, A.A.; Wang, H.; Pierce, D.T. Impact of materials properties on higher-temperature engine operation. SAE Int. J. Adv. Curr. Pract. Mobil. 2021, 4, 448–461. [Google Scholar] [CrossRef] [Scilit]
  13. Zieher, F.; Langmayr, F.; Jelatancev, A.; Wieser, K. Thermal mechanical fatigue simulation of cast iron cylinder heads. In Proceedings of the SAE 2005 World Congress & Exhibition, Detroit, MI, USA, 11 April 2005. [Google Scholar] [CrossRef] [Scilit]
  14. Kulkarni, G.J.; Patra, A. Constitutive model for high temperature deformation of SiMo cast iron: Application to thermo-mechanical fatigue of exhaust manifolds. Int. J. Fatigue 2025, 193, 108776. [Google Scholar] [CrossRef] [Scilit]
  15. Hazime, R.; Seifert, T.; Kessens, J.; Ju, F. Lifetime assessment of cylinder heads for efficient heavy duty engines Part II: Component-level application of advanced models for thermomechanical fatigue life prediction of lamellar graphite cast iron GJL250 and vermicular graphite cast iron GJV450 cyli. SAE Int. J. Engines 2017, 10, 359–365. [Google Scholar] [CrossRef] [Scilit]
  16. Gocmez, T.; Awarke, A.; Pischinger, S. A new low cycle fatigue criterion for isothermal and out-of-phase thermomechanical loading. Int. J. Fatigue. 2010, 32, 769–779. [Google Scholar] [CrossRef] [Scilit]
  17. Jing, G.; Sun, S.; Ma, T.; Li, S.; Ma, T.; Wei, J.; Pang, J. Prediction of thermomechanical fatigue life in RuT450 compacted graphite cast iron cylinder heads using the Neu/Sehitoglu model. Eng. Fail. Anal. 2024, 156, 107767. [Google Scholar] [CrossRef] [Scilit]
  18. Terčelj, M.; Burja, J.; Kugler, G.; Mrvar, P. Thermal fatigue degradation progress in SiMo ductile cast iron under oxidation conditions. Eng. Fail. Anal. 2024, 156, 107823. [Google Scholar] [CrossRef] [Scilit]
  19. Zhang, Q.; Zuo, Z.; Liu, J. Failure analysis of a diesel engine cylinder head based on finite element method. Eng. Fail. Anal. 2013, 34, 51–58. [Google Scholar] [CrossRef] [Scilit]
  20. Dong, C.; Qu, S.; Li, S.X.; Pang, J.C.; Zhang, Z.F.; Fu, C.M.; Xu, C.G.; Zhang, M.X.; Jing, G.X. Investigation into diesel engine cylinder head failure. Eng. Fail. Anal. 2018, 90, 36–46. [Google Scholar] [CrossRef] [Scilit]
  21. Wu, Y.; Li, J.; Yang, Z.; Guo, Y.; Ma, Z.; Liang, M.; Yang, T.; Tao, D. Creep behavior accompanying oxidation of compacted graphite cast iron. Mater. Sci. Eng. A 2018, 723, 174–181. [Google Scholar] [CrossRef] [Scilit]
  22. Jing, G.; Li, S.; Chen, G.; Wei, J.; Sun, S.; Zhang, J. Research on creep test of compacted graphite cast iron and parameter identification of constitutive model under wide range of temperature and stress. Appl. Sci. 2022, 12, 5032. [Google Scholar] [CrossRef] [Scilit]
  23. Joshi, A.; Baxevanakis, K.P.; Silberschmidt, V.V. High-Temperature Creep of Cast Irons. In Solid Mechanics, Theory of Elasticity and Creep; Altenbach, H., Mkhitaryan, S.M., Hakobyan, V., Sahakyan, A.V., Eds.; Springer International Publishing: Cham, Switzerland, 2023; pp. 147–173. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  24. Mohammadpour, A.; Geers, M.G.D.; Kouznetsova, V.G. Multi-scale modeling of the thermo-mechanical behavior of cast iron. Multiscale Sci. Eng. 2022, 4, 119–136. [Google Scholar] [CrossRef] [Scilit]
  25. Joshi, A.; Baxevanakis, K.P.; Silberschmidt, V.V. High-temperature creep in compacted graphite iron: Tension vs. Compression. Eng. Fail. Anal. 2025, 182, 110052. [Google Scholar] [CrossRef] [Scilit]
  26. Zhang, Y.Y.; Pang, J.C.; Shen, R.L.; Qiu, Y.; Li, S.X.; Zhang, Z.F. Investigation on tensile deformation behavior of compacted graphite iron based on cohesive damage model. Mater. Sci. Eng. A 2018, 713, 260–268. [Google Scholar] [CrossRef] [Scilit]
  27. Cavallini, M.; Di Bartolomeo, O.; Iacoviello, F. Fatigue crack propagation damaging micromechanisms in ductile cast irons. Eng. Fract. Mech. 2008, 75, 694–704. [Google Scholar] [CrossRef] [Scilit]
  28. Iacoviello, F.; Di Cocco, V.; Bellini, C. Fatigue crack propagation and damaging micromechanisms in Ductile Cast Irons. Int. J. Fatigue 2019, 124, 48–54. [Google Scholar] [CrossRef] [Scilit]
  29. Sjögren, T.; Svensson, I.L. Modelling the effect of graphite morphology on the modulus of elasticity in cast irons. Int. J. Cast. Met. Res. 2004, 17, 271–279. [Google Scholar] [CrossRef] [Scilit]
  30. Khalid, M.Y.; Umer, R.; Khan, K.A. Review of recent trends and developments in aluminium 7075 alloy and its metal matrix composites (MMCs) for aircraft applications. Results Eng. 2023, 20, 101372. [Google Scholar] [CrossRef] [Scilit]
  31. Guo, C.; Wang, J.; Wang, Y.; Wang, D.; Tan, C.; Zhang, H.; Chen, P.; Sun, J.; Lv, Z. Nickel-based superalloy matrix composites fabricated by laser additive manufacturing: A critical review of recent advances and overcoming challenges. J. Alloys Compd. 2025, 1048, 185331. [Google Scholar] [CrossRef] [Scilit]
  32. Barbera, D.; Chen, H.; Liu, Y. Creep-fatigue behaviour of aluminum alloy-based metal matrix composite. Int. J. Press. Vessel. Pip. 2016, 139–140, 159–172. [Google Scholar] [CrossRef] [Scilit]
  33. Dey, A.P.; Welschinger, F.; Schneider, M.; Gajek, S.; Böhlke, T. Rapid inverse calibration of a multiscale model for the viscoplastic and creep behavior of short fiber-reinforced thermoplastics based on Deep Material Networks. Int. J. Plast. 2023, 160, 103484. [Google Scholar] [CrossRef] [Scilit]
  34. Kovačević, D.; Hofman, P.; Rocha, I.B.C.M.; Van Der Meer, F.P. Unifying creep and fatigue modeling of composites: A time-homogenized micromechanical framework with viscoplasticity and cohesive damage. J. Mech. Phys. Solids 2024, 193, 105904. [Google Scholar] [CrossRef] [Scilit]
  35. Kong, X.; Wang, Y.; Yang, R. Creep deformation of unidirectional metal matrix composites: Modeling and experimental observations. Int. J. Plast. 2025, 192, 104407. [Google Scholar] [CrossRef] [Scilit]
  36. Shishvan, S.S. High-temperature tensile and creep behavior of Cu-Nb composites: A discrete dislocation plasticity investigation. Int. J. Plast. 2021, 136, 102876. [Google Scholar] [CrossRef] [Scilit]
  37. Rodriguez, F.J.; Boccardo, A.D.; Dardati, P.M.; Celentano, D.J.; Godoy, L.A. Thermal expansion of a spheroidal graphite iron: A micromechanical approach. Finite Elem. Anal. Des. 2018, 141, 26–36. [Google Scholar] [CrossRef] [Scilit]
  38. Andriollo, T.; Thorborg, J.; Hattel, J. Modeling the elastic behavior of ductile cast iron including anisotropy in the graphite nodules. Int. J. Solids Struct. 2016, 100–101, 523–535. [Google Scholar] [CrossRef] [Scilit]
  39. Bartošák, M.; Horváth, J. A continuum damage coupled unified viscoplastic model for simulating the mechanical behaviour of a ductile cast iron under isothermal low-cycle fatigue, fatigue-creep and creep loading. Int. J. Plast. 2024, 173, 103868. [Google Scholar] [CrossRef] [Scilit]
  40. Xiao, B.; Yadav, S.D.; Zhao, L.; Tang, Z.; Han, Y.; Yang, X.; Kai, J.J.; Yang, T.; Xu, L. Deep insights on the creep behavior and mechanism of a novel G115 steel: Micromechanical modeling and experimental validation. Int. J. Plast. 2021, 147, 103124. [Google Scholar] [CrossRef] [Scilit]
  41. Fernandino, D.O.; Cisilino, A.P.; Boeri, R.E. Determination of effective elastic properties of ferritic ductile cast iron by computational homogenization, micrographs and microindentation tests. Mech. Mater. 2015, 83, 110–121. [Google Scholar] [CrossRef] [Scilit]
  42. Norman, V.; Calmunger, M. On the micro- and macroscopic elastoplastic deformation behaviour of cast iron when subjected to cyclic loading. Int. J. Plast. 2019, 115, 200–215. [Google Scholar] [CrossRef] [Scilit]
  43. Matsushita, T.; Domeij, B.; Fourlakidis, V.; Belov, I.; Diószegi, A. A model for the effect of microstructure on the ultimate tensile strength of cast irons. Int. J. Met. 2025, 19, 1369–1377. [Google Scholar] [CrossRef] [Scilit]
  44. Andriollo, T.; Hattel, J. On the isotropic elastic constants of graphite nodules in ductile cast iron: Analytical and numerical micromechanical investigations. Mech. Mater. 2016, 96, 138–150. [Google Scholar] [CrossRef] [Scilit]
  45. Bonora, N.; Ruggiero, A. Micromechanical modeling of ductile cast iron incorporating damage. Part I: Ferritic ductile cast iron. Int. J. Solids Struct. 2005, 42, 1401–1424. [Google Scholar] [CrossRef] [Scilit]
  46. Collini, L.; Pirondi, A. Microstructure-based RVE modeling of the failure behavior and LCF resistance of ductile cast iron. Procedia Struct. Integr. 2019, 24, 324–336. [Google Scholar] [CrossRef] [Scilit]
  47. Hütter, G.; Zybell, L.; Kuna, M. Micromechanisms of fracture in nodular cast iron: From experimental findings towards modeling strategies—A review. Eng. Fract. Mech. 2015, 144, 118–141. [Google Scholar] [CrossRef] [Scilit]
  48. Rizzoni, R.; Livieri, P.; Tovo, R.; Cova, M. Development of a hierarchical model for voids clusters suitable for cast iron degenerated graphite. Theor. Appl. Fract. Mech. 2020, 109, 102731. [Google Scholar] [CrossRef] [Scilit]
  49. Dong, M.J.; Prioul, C.; François, D. Damage effect on the fracture toughness of nodular cast iron: Part I. Damage characterization and plastic flow stress modeling. Metall. Mater. Trans. A 1997, 28, 2245–2254. [Google Scholar] [CrossRef] [Scilit]
  50. Palkanoglou, E.N.; Baxevanakis, K.P.; Silberschmidt, V.V. Thermal debonding in compacted graphite iron: Effect of interaction of graphite inclusions. Procedia Struct. Integr. 2022, 37, 209–216. [Google Scholar] [CrossRef] [Scilit]
  51. Dassault Systèmes, S.E. Abaqus/Standard. 2023. Available online: https://help.3ds.com/ (accessed on 6 March 2026).
  52. Betten, J. Creep Mechanics, 3rd ed.; Springer: Berlin/Heidelberg, Germany, 2008. [Google Scholar] [CrossRef] [Scilit]
  53. Penny, R.K.; Marriott, D.L. Design for Creep, 2nd ed.; Springer: Dordrecht, The Netherlands, 1995. [Google Scholar] [CrossRef] [Scilit]
  54. Yang, B.; Xuan, F.-Z.; Jiang, W.-C. On the interrupted creep test under low stress levels for the power law parameter extraction. J. Press. Vessel Technol. 2020, 142, 2–7. [Google Scholar] [CrossRef] [Scilit]
  55. Sattar, M.; Othman, A.R.; Kamaruddin, S.; Akhtar, M.; Khan, R. Limitations on the computational analysis of creep failure models: A review. Eng. Fail. Anal. 2022, 134, 105968. [Google Scholar] [CrossRef] [Scilit]
  56. Naumenko, K.; Altenbach, H. Modeling High Temperature Materials Behavior for Structural Analysis; Springer International Publishing: Cham, Switzerland, 2016. [Google Scholar] [CrossRef] [Scilit]
  57. Jin, S.; Harmuth, H.; Gruber, D. Compressive creep testing of refractories at elevated loads-Device, material law and evaluation techniques. J. Eur. Ceram. Soc. 2014, 34, 4037–4042. [Google Scholar] [CrossRef] [Scilit]
  58. Dowling, N.E. Mechanical Behavior of Materials, 4th ed.; Pearson Education Limited: London, UK, 2013. [Google Scholar]
  59. Nektaria Palkanoglou, E.; Baxevanakis, K.P.; Silberschmidt, V.V. Thermal debonding of inclusions in compacted graphite iron: Effect of matrix phases. Eng. Fail. Anal. 2022, 139, 106476. [Google Scholar] [CrossRef] [Scilit]
  60. Cao, M.; Palkanoglou, E.N.; Baxevanakis, K.P.; Silberschmidt, V.V. Thermomechanical behaviour and damage in CGI: 3D finite-element analysis. Eng. Fract. Mech. 2025, 325, 111317. [Google Scholar] [CrossRef] [Scilit]
  61. Pina, J.C.; Kouznetsova, V.G.; Geers, M.G.D. Elevated temperature creep of pearlitic steels: An experimental–numerical approach. Mech. Time-Depend. Mater. 2014, 18, 611–631. [Google Scholar] [CrossRef] [Scilit]
  62. Firoozbakht, M.; Horbach, L.; Weber, F.; Štěpán, R.; Zhang, J.; Pustal, B.; Broeckmann, C.; Bührig-Polaczek, A. Linking cooling conditions, pearlite characteristics, and mechanical properties in pearlitic ductile cast iron: Experimental and simulation insights. Mater. Des. 2026, 264, 115693. [Google Scholar] [CrossRef] [Scilit]
  63. Fourlakidis, V.; Diószegi, A. A generic model to predict the ultimate tensile strength in pearlitic lamellar graphite iron. Mater. Sci. Eng. A 2014, 618, 161–167. [Google Scholar] [CrossRef] [Scilit]
  64. Grote, K.-H.; Antonsson, E.K. (Eds.) Springer Handbook of Mechanical Engineering; Springer: Berlin/Heidelberg, Germany, 2009. [Google Scholar] [CrossRef] [Scilit]
  65. Cottrell, A. An Introduction to Metallurgy; The Institute of Materials: London, UK, 1995. [Google Scholar] [CrossRef] [Scilit]
  66. Fomin, Y.D.; Brazhkin, V.V. Comparative study of melting of graphite and graphene. Carbon 2020, 157, 767–778. [Google Scholar] [CrossRef] [Scilit]
  67. Savvatimskiy, A.I. Measurements of the melting point of graphite and the properties of liquid carbon (a review for 1963–2003). Carbon 2005, 43, 1115–1142. [Google Scholar] [CrossRef] [Scilit]
  68. Fischbach, D.B. High-temperature creep of graphite. Nature 1960, 186, 795–797. [Google Scholar] [CrossRef] [Scilit]
  69. Sarkar, A.; Eapen, J.; Raj, A.; Murty, K.L.; Burchell, T.D. Modeling irradiation creep of graphite using rate theory. J. Nucl. Mater. 2016, 473, 197–205. [Google Scholar] [CrossRef] [Scilit]
  70. Tzelepi, A.; Dinsdale-Potter, J.; Wilkinson, S.; Shaw, T.L.; Davies, B.C.; Davies, M.A. Studies of irradiation creep on core graphite by thermal annealing. J. Nucl. Mater. 2020, 539, 152309. [Google Scholar] [CrossRef] [Scilit]
  71. Marsden, B.J.; Haverty, M.; Bodel, W.; Hall, G.N.; Jones, A.N.; Mummery, P.M.; Treifi, M. Dimensional change, irradiation creep and thermal/mechanical property changes in nuclear graphite. Int. Mater. Rev. 2016, 61, 155–182. [Google Scholar] [CrossRef] [Scilit]
  72. Wu, Y.; Li, J.; Chen, H.; Ma, J.; Yang, Z.; Guo, Y.; Liang, M. Creep deformation and damage mechanism of compact graphite cast iron with different pearlite contents. J. Mater. Res. Technol. 2023, 23, 5031–5039. [Google Scholar] [CrossRef] [Scilit]
  73. Ruggiero, A.; Khademi, E. Micromechanical modeling for predicting residual stress–strain state around nodules in ductile cast irons. Metals 2023, 13, 1874. [Google Scholar] [CrossRef] [Scilit]
  74. Pina, J.C.; Kouznetsova, V.G.; van Maris, M.P.F.H.L.; Geers, M.G.D. Microstructural model for the time-dependent thermomechanical analysis of cast irons. GAMM-Mitteilungen 2015, 38, 248–267. [Google Scholar] [CrossRef] [Scilit]
  75. ASTM E2567-16a; Standard Test Method for Determining Nodularity and Nodule Count in Ductile Iron Using Image Analysis. ASTM International: West Conshohocken, PA, USA, 2016. [CrossRef] [Scilit]
  76. Omairey, S.L.; Dunning, P.D.; Sriramula, S. Development of an ABAQUS plugin tool for periodic RVE homogenisation. Eng. Comput. 2019, 35, 567–577. [Google Scholar] [CrossRef] [Scilit]
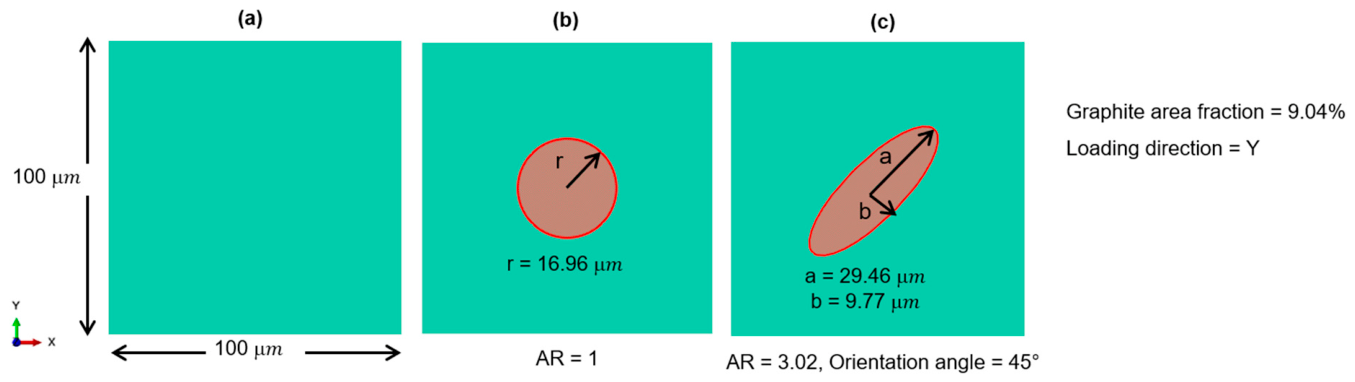
Figure 4. RVE model geometries for creep simulations: (a) matrix only; (b) circular particle; (c) elliptical particle.
Applsci 16 07894 g004
Figure 6. Evolution of creep strain with time: comparison of test data and simulation results.
Applsci 16 07894 g006
Figure 9. Stress redistribution along the paths in Figure 7 at t = 0.01 h: (a) tensile loading; (b) compressive loading.
Applsci 16 07894 g009
Figure 10. Axial stresses at t = 100.01 h for CV models.
Applsci 16 07894 g010
Figure 11. Creep strains at t = 100.01 h for CV models.
Applsci 16 07894 g011
Figure 16. RVE models with elliptical particle to study effects of particle orientation.
Applsci 16 07894 g016
Figure 18. Absolute magnitudes of strains after stage 2 for different particle orientations: (a) maximum plastic strain (PEEQ); (b) maximum creep strain (CEEQ); (c) maximum total strain (E22).
Applsci 16 07894 g018
Figure 23. Effect of particle aspect ratio on the normalised peak axial residual stresses (S22).
Applsci 16 07894 g023
Table 1. Elastic properties for CGI matrix and graphite at 500 °C.
MaterialYoungs Modulus
(GPa)
Poisson’s RatioCoefficient of
Thermal Expansion
Matrix1250.251.5 × 10−5
Graphite15.850.22.9 × 10−6
Table 2. Creep parameters for matrix at 500 °C.
Loading RegimeCreep Parameters
from Experiments
Creep Parameters Used
in Simulations
nmAnCp
Tension6.3150.431.88 × 10−186.3158.04 × 10−19−0.57
Compression3.1820.419.18 × 10−123.1823.77 × 10−12−0.59
Table 3. Matrix creep parameters used for confirmation of simulation methodology.
Load RegimeTemperature (°C)Stress
(MPa)
Creep Parameters
from Experiments
Creep Parameters Used
in Simulations
nmAnCp
Tension4502256.3150.355.19 × 10−196.3151.84 × 10−19−0.65
Table 4. Model notation.
Model DescriptionInclusion ModelModel Category Name Matrix
Modelling
Specific Model Name
Matrix with circular voidsVoidCV ModelsElasticEM-CV
ViscoelasticVEM-CV
ViscoplasticVPM-CV
Matrix with circular graphite inclusionsSolid graphiteG ModelsViscoplasticVPM-CG
Matrix with elliptical graphite inclusionsViscoplasticVPM-EG
Table 5. Effect of stress concentration on creep strains.
ParameterTensile Loading Compressive Loading
Axial stress in matrix-only model after stage 1 (MPa)150−150
Axial stress in VPM-CV model after stage 1 (MPa)310.4−379.4
Stress concentration factor (Kt) based on axial stress2.072.53
Equivalent creep strain (CEEQ) in matrix-only model after stage 2 (mm/mm)7.4 × 10−45.1 × 10−4
Maximum CEEQ in VPM-CV model after stage 2 (mm/mm)3.9 × 10−27.0 × 10−3
Strain concentration factor (Kε) after stage 252.713.7
Table 6. Comparison of maximum local values of axial stresses and creep strains for different graphite modelling approaches.
ResultsTensile LoadingCompressive Loading
t = 0.01 ht = 100.01 ht = 0.01 ht = 100.01 h
Axial stress in VPM-CV model (MPa)310.4282.6−379.4−338.3
Axial stress in VPM-CG model (MPa)268.1187.7−327.5−241.6
Creep strain CEEQ in VPM-CV model (mm/mm)5.87 × 10−33.93 × 10−21.23 × 10−47.00 × 10−3
Creep strain CEEQ in VPM-CG model (mm/mm)2.65 × 10−34.92 × 10−37.54 × 10−52.96 × 10−3
Table 7. Maximum local creep strain results comparisons between plane-stress and plane-strain models.
Graphite Model Tensile LoadingCompressive Loading
Maximum Local Creep Strain CEEQ (mm/mm)CEEQ Ratio for Plane Strain to Plane StressMaximum Local Creep Strain CEEQ (mm/mm)CEEQ Ratio for Plane Strain to Plane Stress
Plane StressPlane StrainPlane StressPlane Strain
No graphite (matrix only)7.43 × 10−43.52 × 10−40.55.12 × 10−43.51 × 10−40.7
Circular solid4.92 × 10−33.88 × 10−30.82.96 × 10−32.45 × 10−30.8
Elliptical solid at 45°4.77 × 10−34.60 × 10−30.963.38 × 10−33.08 × 10−30.9
Table 8. Axial stress results from viscoplastic model with realistic particle at key locations identified in Figure 25.
LocationS22 in Tension (MPa)S22 in Compression (MPa)
t = 0.01 ht = 100.01 ht = 0.01 ht = 100.01 h
A351.1197.9−511.7−169.9
B348.6176.2−514.1−165.4
C238.6181.5−268.5−216.2
D352.4186.9−484.3−259.5
Table 9. Comparison of maximum creep strains after stage 2 with different inclusion shapes.
Inclusion ShapeMaximum Plastic Strain (mm/mm)Maximum Creep Strain (mm/mm)Maximum Total Strain (mm/mm)
TensionCompressionTensionCompressionTensionCompression
Idealised—circular1.5 × 10−35.9 × 10−44.9 × 10−33.0 × 10−37.9 × 10−35.5 × 10⁻³
Idealised—45° elliptical2.6 × 10−31.4 × 10−34.8 × 10−33.4 × 10−38.8 × 10−36.7 × 10⁻³
Idealised—0° elliptical5.3 × 10−33.5 × 10−34.3 × 10−34.0 × 10−31.1 × 10−29.6 × 10⁻³
Realistic1.2 × 10−21.1 × 10−25.1 × 10−33.8 × 10−31.4 × 10−21.5 × 10⁻²
Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content.