Article

Multi-Hazard Performance and Failure Mechanisms of Repair Techniques for Full-Diameter Damaged Agricultural Steel Pipelines


1
Department of Agricultural and Rural Engineering, Chungnam University, Daejeon 34134, Republic of Korea
2
Research and Development Centre, Construction Material Test Laboratory Co., Ltd., Eumseong-gun 27734, Republic of Korea
3
Department of Agricultural Civil Engineering, Kyungpook National University, Daegu 41566, Republic of Korea
*
Authors to whom correspondence should be addressed.
Appl. Sci. 2026, 16(15), 7761; https://doi.org/10.3390/app16157761
Submission received: 5 July 2026 / Revised: 24 July 2026 / Accepted: 1 August 2026 / Published: 4 August 2026
(This article belongs to the Section Civil Engineering)

Featured Application

The proposed FRP wrapping and overlay welding techniques can be applied to the rehabilitation of aging steel pipelines in agricultural irrigation systems, providing practical solutions to restore structural integrity, maintain hydraulic performance, and enhance long-term durability against corrosion in aggressive service environments.

Abstract

Although steel pipelines constitute the primary infrastructure of agricultural irrigation systems, they are highly susceptible to moisture-induced pitting corrosion and severe operational conditions, including internal pressure fluctuations and heavy overburden loads. This study evaluated the structural performance and durability of full-diameter steel pipe specimens (311.5 mm in diameter and 2.0 m long) repaired using CFRP (single-layer) and GFRP (single- and multi-layer) sheet wrapping as well as overlay welding. A 60-mm pinhole defect corresponding to a 6% circumferential damage ratio was introduced to simulate advanced localized corrosion. The repaired pipelines were experimentally assessed under four-point bending, internal hydrostatic pressure, and accelerated salt spray exposure. Under service-level flexural loading, all specimens exhibited similar global load–deflection responses regardless of defect or repair condition. However, localized strain measurements revealed that the unrepaired defect produced tensile strains up to 12 times greater than those of the intact pipe, whereas all repair techniques effectively suppressed the localized strain concentration. The effectiveness of the FRP systems improved with increasing reinforcement thickness. Overlay welding provided the highest structural performance, restoring localized strain behavior to a level comparable to that of the intact pipe. Under an internal pressure of 2.0 MPa, welding and CFRP maintained 100% pressure retention, whereas single-layer GFRP exhibited minor radial bulging, reducing its pressure retention ratio to 73.5%. Increasing the GFRP thickness restored the retention ratio to 93.0%. Accelerated salt spray exposure further demonstrated that GFRP provided effective barrier protection against corrosion by acting as an impermeable dielectric barrier under short-term exposure, whereas welded specimens still exhibited localized corrosion around the heat-affected zone despite epoxy coating. These findings demonstrate that overlay welding offers the greatest immediate structural restoration, whereas adequately dimensioned FRP systems can provide a more balanced solution for multi-hazard durability by simultaneously enhancing structural performance and mitigating electrochemical degradation in aging agricultural steel pipelines.

1. Introduction

Steel pipelines constitute the critical structural backbone of agricultural irrigation and water conveyance networks owing to their high tensile capacity, robust hydraulic performance, and adaptability [1]. However, these buried infrastructures operate in highly aggressive underground environments, characterized by corrosive soil moisture, internal pressure fluctuations, and heavy over-burden loads. Prolonged exposure to moisture, dissolved oxygen, and soil electrolytes relentlessly induces progressive electrochemical deterioration, predominantly manifesting as highly localized pitting corrosion [2]. Over time, this localized section loss evolves into critical perforations or pinhole defects. Such geometric discontinuities act as severe stress concentrators that not only drastically degrade the structural load-bearing capacity of the pipeline, but also serve as direct conduits for fluid leakage, plunging the operational efficiency and inflating maintenance costs [3,4,5,6,7].
Various repair and strengthening techniques, including pipe replacement, surface coating, overlay welding, and advanced fiber-reinforced polymer (FRP) composite wrapping, have been applied to restore the integrity of deteriorated steel pipes [8,9,10]. Direct overlay welding has long been the conventional gold standard in pipeline rehabilitation [2]. By physically reconstituting the missing steel section, welding metallurgically restores both the structural load path and full hydraulic containment. However, the execution of high-quality field welding on aging, pressurized large-diameter mains demands extensive excavation, specialized labor, and disruptive service interruptions [8]. Furthermore, the welding thermal cycles inherently introduce heat-affected zones (HAZs) and stiffness mismatches that may alter local ductility. Consequently, a paradigm shift toward non-hot-work, externally applied composite repair/strengthening systems has gained significant momentum.
Fiber-reinforced polymer (FRP) composites have emerged as one of the most promising alternatives. FRP materials possess high strength-to-weight ratios, excellent corrosion resistance, lightweight characteristics, and ease of installation, making them attractive for the rehabilitation of deteriorated steel structures [11,12,13,14]. In particular, carbon fiber-reinforced polymer (CFRP) provides high stiffness and strength, whereas glass fiber-reinforced polymer (GFRP) offers superior deformability and cost-effectiveness [15,16]. Previous studies have demonstrated that FRP retrofitting can effectively enhance the strength and stiffness of damaged steel members while mitigating stress concentration effects [17,18,19]. Furthermore, recent experimental evaluations have confirmed that composite wrapping substantially restores the pressure retention capacity of steel pipelines with severe through-wall defects, where the failure pressure is strongly governed by reinforcement layer thickness, fiber type, and defect geometry [20]. Additionally, recent investigations on composite-repaired steel members have highlighted that optimizing fiber architecture and adhesive layer characteristics plays a pivotal role in maximizing fatigue life and preventing environmental degradation [21,22,23]. Consequently, FRP retrofitting can be installed without large-scale excavation or heat-based processes such as welding, making it a promising maintenance solution for aging pipeline systems [2,14,15,16,24].
Despite the widespread utilization of both metallurgical (welding) and adhesive (FRP) repair paradigms, the current literature presents critical research gaps [14,19,20]. First, the majority of prior studies have either evaluated these methods in isolation or relied on small-diameter scaled models [19,20]. The fundamental stress-transfer mechanisms and debonding thresholds of FRP composites are highly sensitive to geometric scaling; the localized stress singularities and immense hoop tensions generated in large-diameter pipelines may completely overwhelm repair configurations that perform adequately at smaller scales [14]. Second, existing comparative studies have predominantly focused on a single performance metric—typically structural strength under static loading [14,19]. However, an in-service buried pipeline simultaneously faces several severe operational hazards, such as transverse bending moments induced by soil overburden and traffic loads, massive internal hydrostatic pressures capable of triggering catastrophic blow-outs, and continuous exposure to aggressive corrosive environments [14]. A holistic, cross-disciplinary evaluation assessing structural recovery, water-tightness, and long-term durability under identical severe damage conditions remains scarce. Although evaluations of various repair methods for aging agricultural steel pipes have recently been conducted [25], detailed analytical interpretations regarding stress-transfer mechanisms and scale effects remain limited.
To address these critical knowledge gaps and provide robust, performance-based engineering guidelines, this study experimentally evaluates the structural, hydraulic, and durability performance of full-diameter agricultural steel pipe specimens (approximately 300 mm in diameter) repaired with different techniques. Building upon foundational mechanisms identified in small-diameter models in the preliminary test, a severe localized perforation—corresponding to approximately a 6% circumferential damage ratio—was introduced to simulate advanced pitting corrosion. The specific interventions investigated include overlay welding, single-layer GFRP, multi-layer (3-layer) GFRP, and CFRP composite wraps, intentionally selected to compare varying radial confinement stiffnesses and metallurgical continuity. To capture the full spectrum of in-service demands, the repaired large-diameter pipes were subjected to rigorous four-point bending tests (structural integrity), hydrostatic pressure tests (leak containment and hoop stress resistance), and accelerated salt spray tests (corrosion resistance). By systematically comparing these distinct retrofitting paradigms under multiaxial and multi-hazard conditions, this study aims to establish a quantitative, evidence-based framework for the optimal selection of rehabilitation strategies in aging full-scale pipeline networks.

2. Test Program

2.1. Test Specimens and Repair Configurations

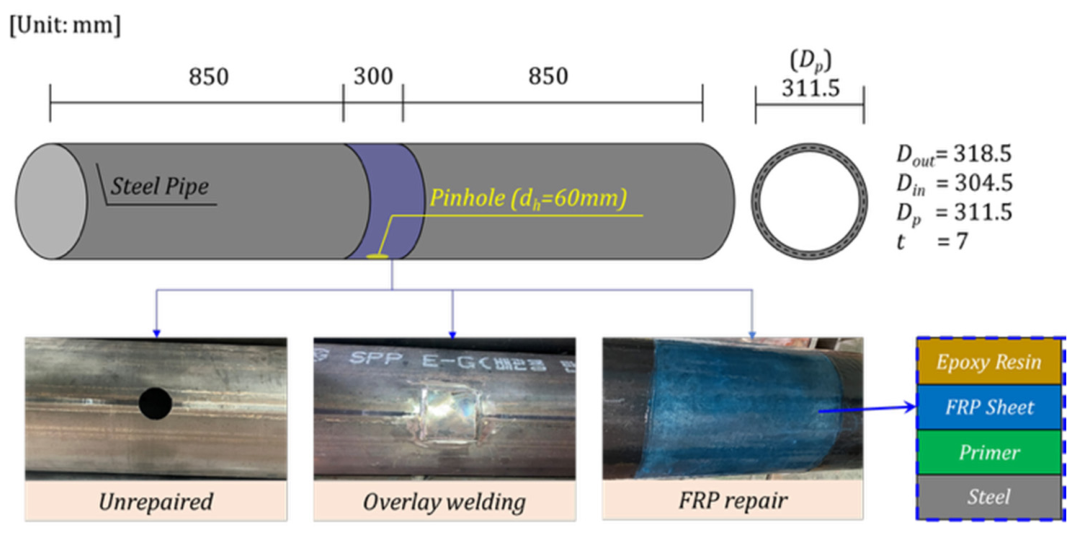
The experimental program utilized full-diameter, non-galvanized carbon steel pipes conforming to KS D 3507 (nominal diameter: 300 A) [26], representing standard large-diameter agricultural transmission mains. The geometric dimensions of the pipes were as follows: outer diameter (Dout) of 318.5 mm, nominal wall thickness (t) of 7 mm, unit weight of 53.8 kg/m, and a total specimen length of 2000 mm. Building upon the critical damage threshold identified in foundational small-diameter studies, localized advanced pitting corrosion was simulated by machining a circular through-hole with a diameter (dh) of 60 mm at the midspan of each specimen. This geometric discontinuity corresponds precisely to a 6% circumferential damage ratio (dh/πDp), which was adopted from prior baseline investigations on small-diameter steel pipes (D ≈ 25 mm) [25,27]. In those studies, a 6% circumferential defect was experimentally verified to induce severe structural degradation—reducing the ultimate load capacity and ductility by approximately 28% and 16%, respectively, compared to intact pipes. By fully mobilizing stress-transfer mechanisms under this sufficiently severe condition, this defect ratio establishes a rigorous comparative baseline for evaluating scale effects and multi-hazard vulnerabilities. Figure 1 shows a schematic illustration of the steel pipe specimen, the artificial pinhole damage, and the repair methods.
The experimental matrix (Table 1) was designed to evaluate the stress-transfer efficacy of different retrofitting schemes. To systematically investigate the influence of radial confinement stiffness and composite modulus, the defect regions were externally wrapped with single-layer GFRP (1-GFRP), triple-layer GFRP (3-GFRP), and single-layer CFRP (1-CFRP). All composite wraps were applied over a bonded length of 300 mm centered on the defect using a wet lay-up process at ambient temperature. Prior to wrapping, the steel surface was uniformly coated with an epoxy primer. The composite sheets were then manually wrapped and consolidated with rollers to ensure complete resin impregnation and eliminate entrapped air bubbles, followed by full ambient curing. For direct comparison with metallurgical restoration, an overlay welding configuration (W) was prepared by fillet-welding a steel patch—matching the original pipe thickness (7 mm)—over the damaged zone. The intrinsic mechanical properties of the FRP fabrics and the epoxy matrix are detailed in Table 2 and Table 3.

2.2. Material Characterization (Extracted Coupon Tests)

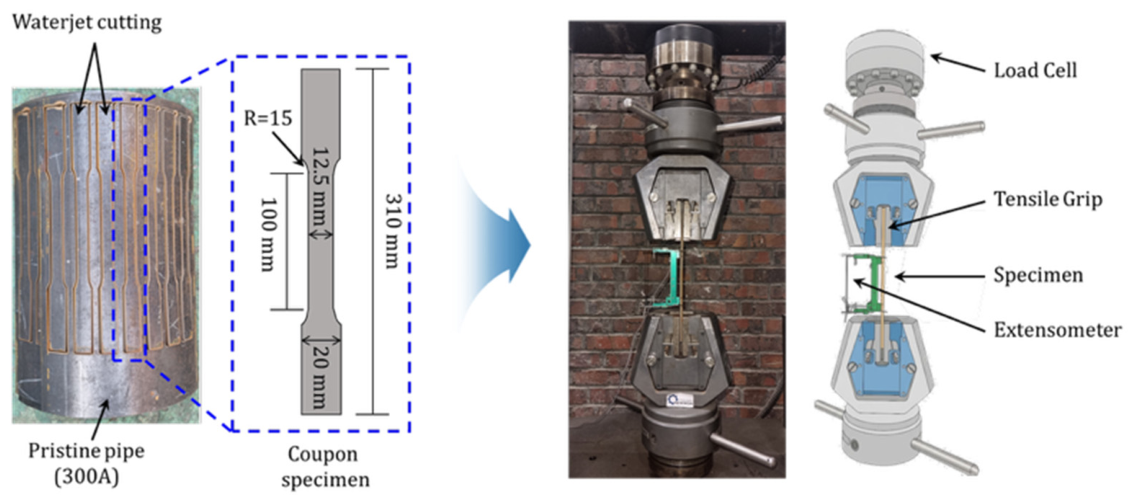
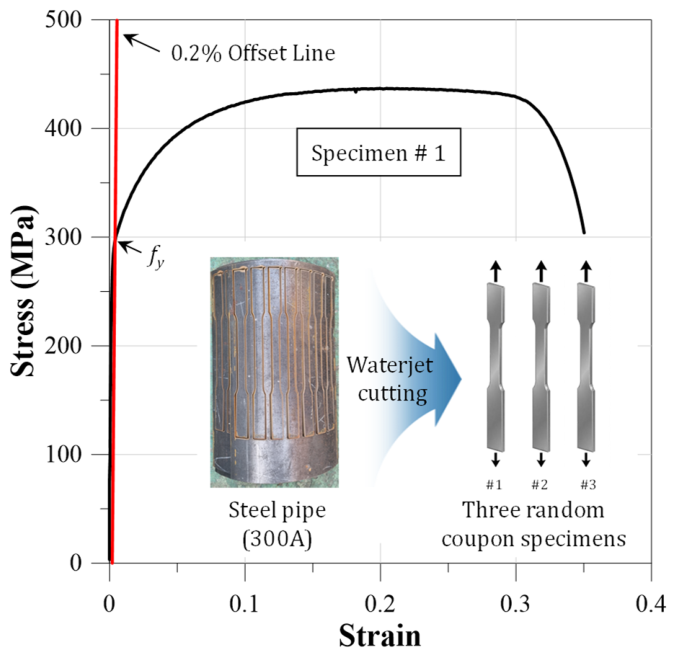
To evaluate the material properties of the steel pipes, tensile coupon specimens were extracted longitudinally from the pristine pipes, as shown in Figure 2. To definitively eliminate the risk of microstructural alterations and residual thermal stresses associated with conventional mechanical or plasma cutting, a precision waterjet cutting technique was strictly employed. The coupon geometries were strictly machined in accordance with ASTM E8/E8M [28]. A total of three replicate specimens were tested utilizing a 200 kN universal testing machine (UTM, Model: 4485, Instron, Norwood, MA, USA). Axial strains were precisely monitored using a 100 mm gauge length extensometer (Model: 3543-200M-050M-ST, Epsilon Technology Corp., Jackson, WY, USA) mounted on the central gauge section.

2.3. Four-Point Bending Test

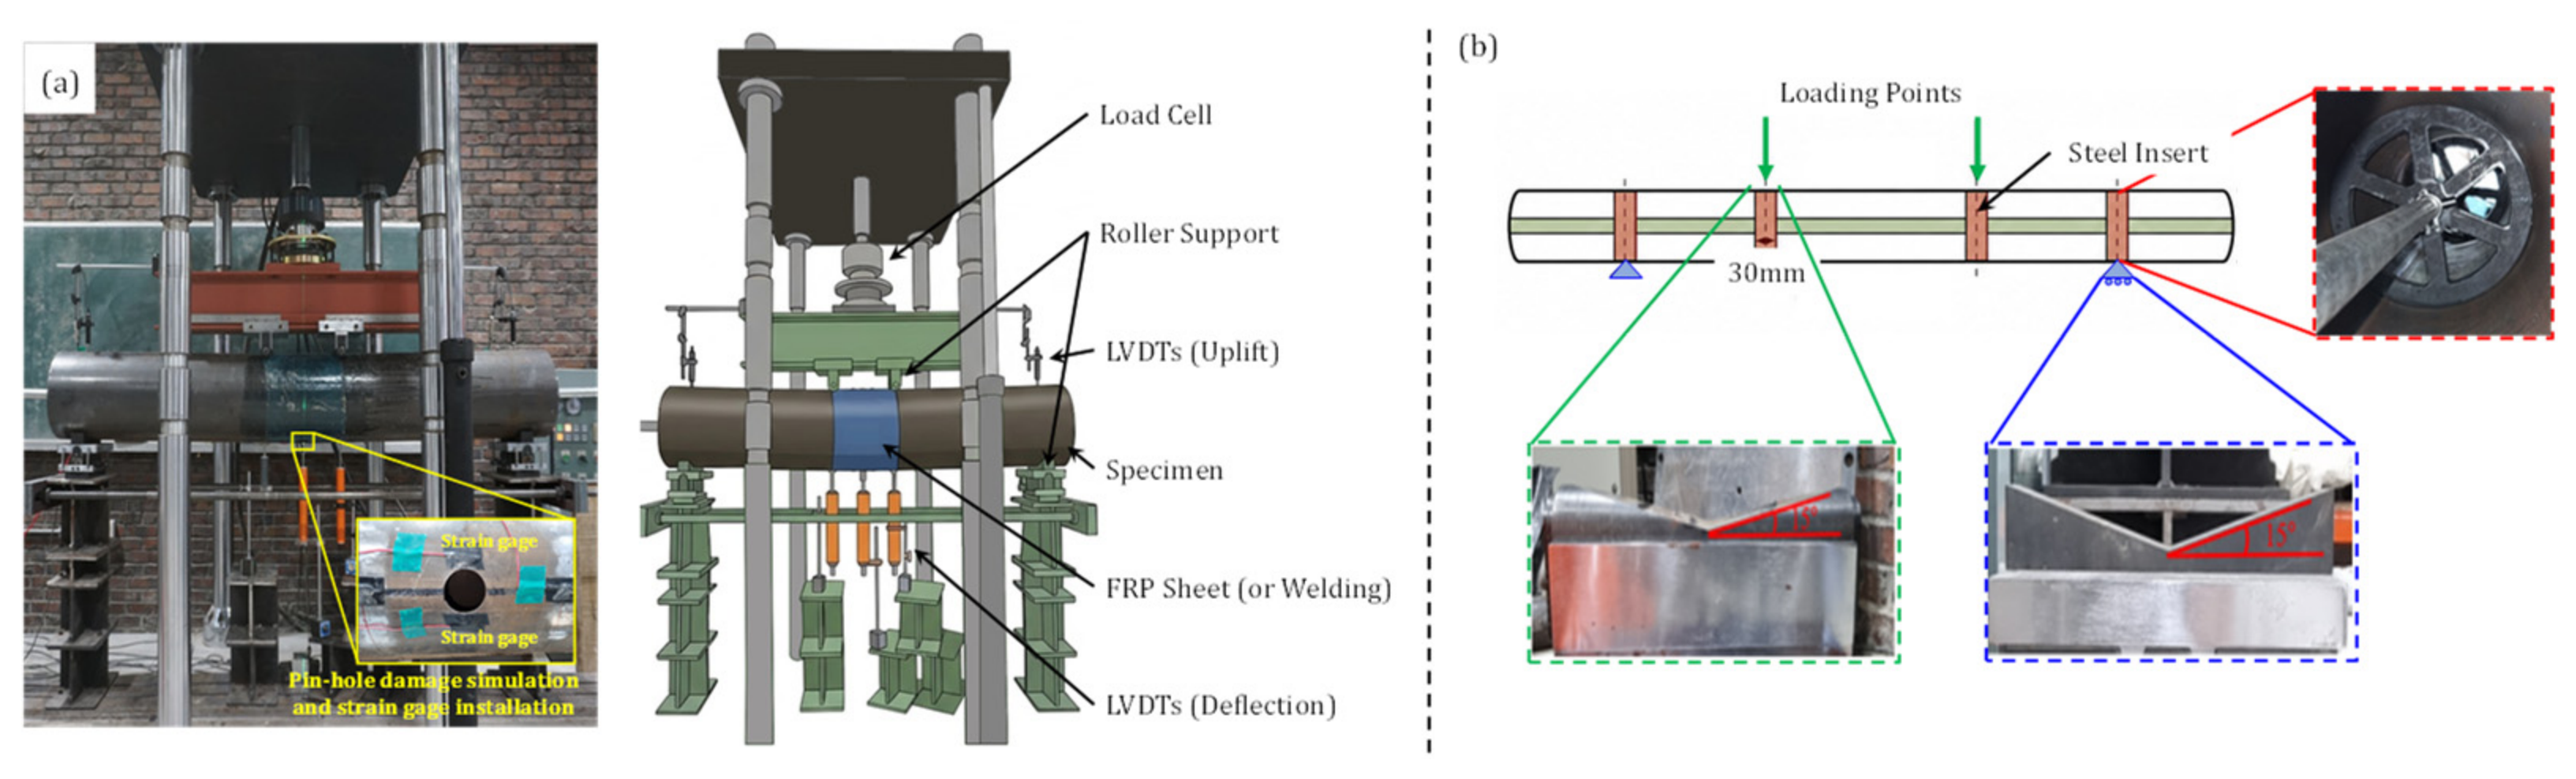
To evaluate the structural integrity and flexural load-path restoration of the repaired pipes under transverse loading (representing soil overburden and dynamic traffic), large-scale four-point bending tests were conducted (Figure 3a). Loading was applied using a 500 kN UTM (Servo UTM, Samyeon Technology Corp., Daegu, Republic of Korea) under displacement control at a rate of 0.5 mm/min. The specimens were simply supported over an effective span of 1800 mm and subjected to a symmetric two-point loading with a 300 mm spacing, creating a constant-moment region at midspan where the artificial defect was located at the extreme tension fiber.
A critical challenge in testing large-diameter thin-walled pipes is premature cross-sectional ovalization and local buckling (web crippling) at the load application points. To circumvent this, custom-fabricated solid steel internal inserts (diameter: 300 mm, thickness: 30 mm) were snug-fitted inside the pipe precisely under the loading points, as shown in Figure 3b. Additionally, the upper loading and lower support rollers were custom-machined with a 15° V-shaped groove. This geometric adaptation ensured uniform bearing contact and effectively distributed the highly concentrated boundary stresses. Deformation kinematics were rigorously monitored using a multi-point LVDT array (Tokyo Measuring Instruments Laboratory, Tokyo, Japan): a 100-mm LVDT (Model CDP-100) tracked global midspan deflection, while sets of 50-mm (CDP-50) and 10-mm LVDTs (CDP-10) monitored local vertical displacements under the loading points and uplift deformations at the supports, respectively (Figure 3a).

2.4. Hydrostatic Pressure Test

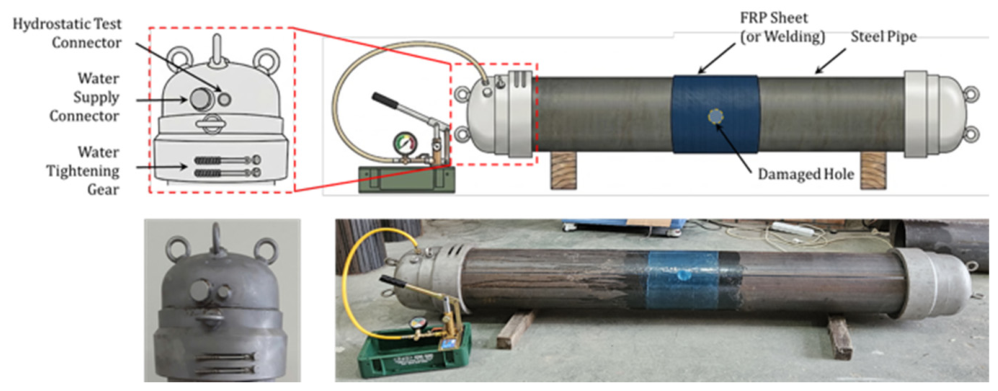
In-service agricultural pipelines are continuously subjected to immense internal hydraulic pressure, generating massive hoop stresses (σh = pr/t). To rigorously evaluate not only the physical leak tightness, but also the interfacial debonding resistance of the external FRP wraps under active hoop tension, a high-pressure hydrostatic test was designed, referencing the protocol proposed by Westra et al. [29] (Figure 4).
The objective of this test was not to reproduce the actual service conditions of agricultural irrigation pipelines, but to evaluate the leakage sealing performance of different repair methods under controlled and comparable conditions. Accordingly, the target pressure was selected based on two criteria: (1) sufficient magnitude to clearly identify leakage, and (2) safe operation within the allowable pressure range specified in KS D 3507 [26]. Considering that the rated hydrostatic pressure of the pipe and testing system was 2.5 MPa, a target pressure of 2.0 MPa (80% of the rated capacity) was adopted. This level was sufficient to assess the confinement effectiveness of the repair systems while remaining within the elastic limit of the steel pipe.
Hydrostatic test caps were installed at both ends to ensure sealed boundary conditions, and the specimens were completely filled with water using a municipal supply line. Residual air was removed by circulating water through a connector port for approximately 10 min to prevent pressure instability and ensure true hydrostatic loading. The internal pressure was then gradually increased to 2.0 MPa and maintained for 60 min. During this period, pressure variation and any leakage around the repaired and damaged regions were continuously monitored to evaluate the watertightness performance of each repair method.

2.5. Salt Spray Test

While external FRP wrapping and welding can restore the initial structural and hydraulic performance, their heterogeneous interfaces (e.g., polymer-to-steel or weld heat-affected zones) may be vulnerable to long-term corrosion and environmental degradation in chloride-rich soils. Therefore, accelerated salt spray testing was conducted to evaluate the corrosion resistance and protective effectiveness of the repair methods under controlled laboratory conditions.
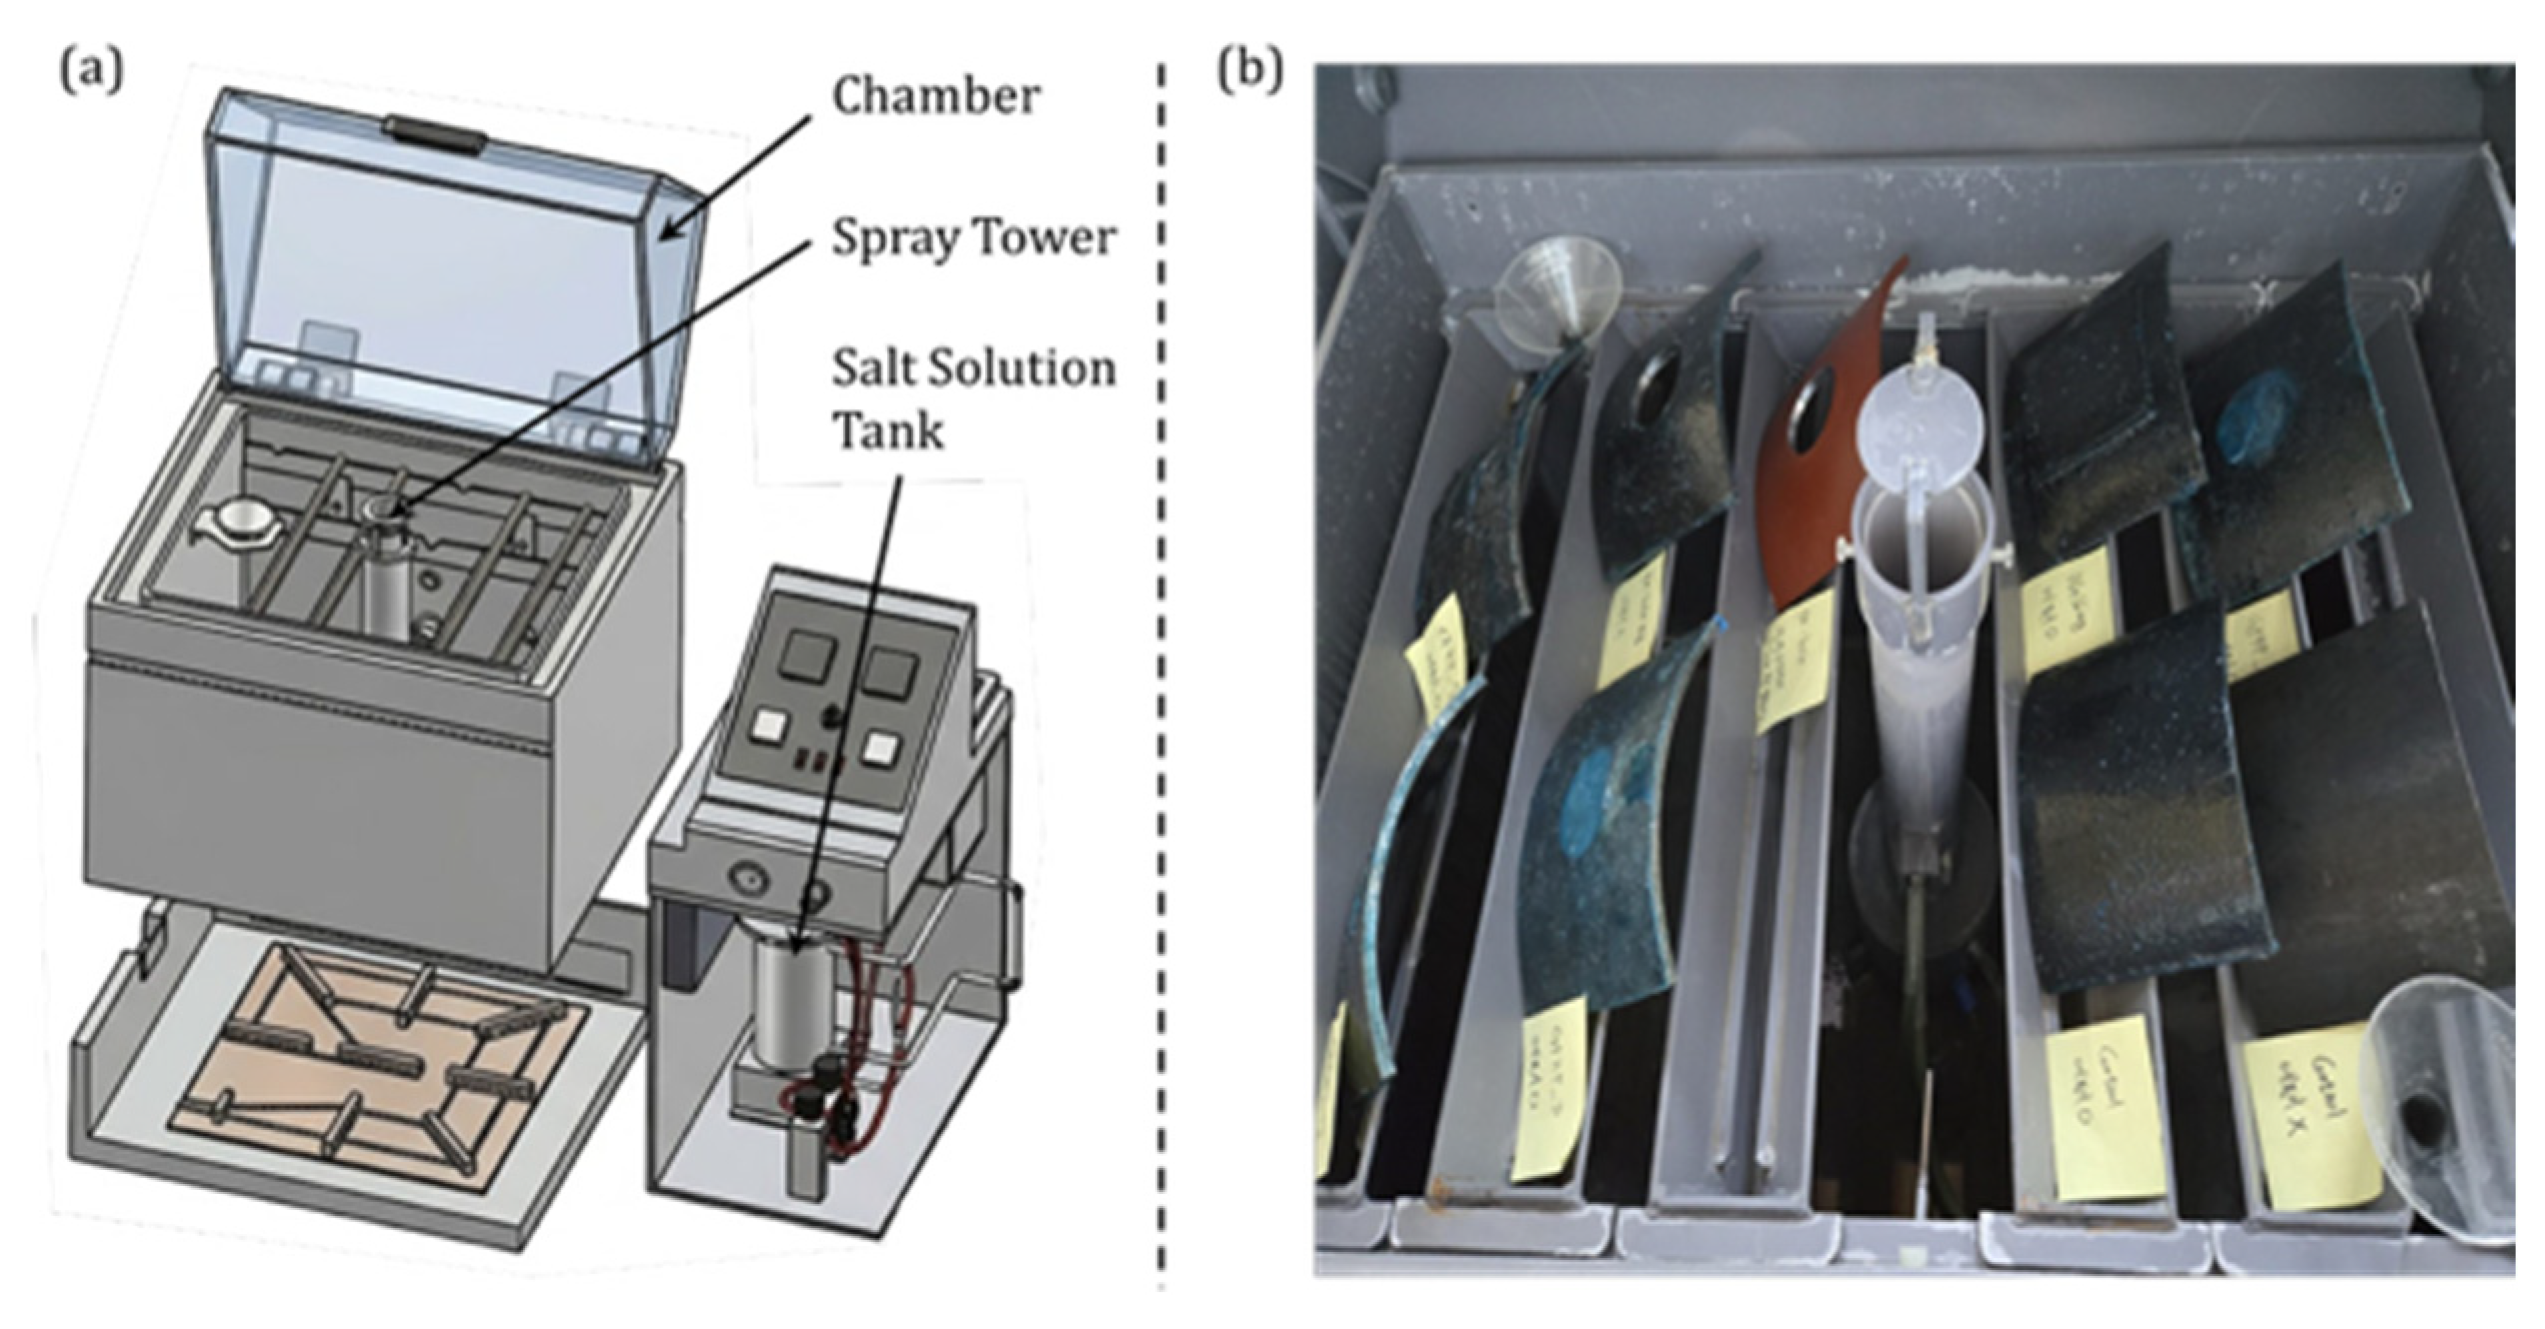
The tests were performed in accordance with ASTM B117 [30] (Figure 5) using a 50 ± 5 g/L NaCl solution with a pH of 6.5–7.2. The chamber temperature was maintained at 35 ± 2 °C, and specimens were continuously exposed to salt fog at a deposition rate of 0.5–1.5 mL/h for 48 h. Specimens were cut from pipes used in the four-point bending tests, with dimensions of 150 mm × 200 mm, and included a centrally located artificial defect (60 mm). The experimental matrix consisted of an unrepaired control, GFRP-wrapped specimens, welded specimens, and an epoxy-coated specimen introduced as a protective coating benchmark (Table 4). It is noted that the specimens repaired with CFRP were excluded from the accelerated salt spray corrosion assessment. This decision was based on the underlying corrosion protection mechanism of externally bonded FRP composite repairs, which is primarily governed by the continuous epoxy resin matrix rather than the specific reinforcement fiber type (CFRP vs. GFRP) [31,32,33]. Consequently, the electrochemical protection mechanism and chloride impermeability remain identical across both composite systems. Furthermore, unlike conventional thin liquid coatings that suffer from edge-thinning and local cracking over sharp defects, the structural fiber fabric acts as a resin carrier, ensuring a thick, uniform encapsulation layer that effectively bridges surface discontinuities. Based on this mechanistic equivalence, GFRP-repaired specimens were utilized as representative samples to evaluate the long-term barrier efficiency and interfacial corrosion resistance of the composite repair system under aggressive chloride exposure.

3. Test Results and Discussions

3.1. Tensile Properties of the Steel Substrate

Tensile tests were conducted on three coupon specimens extracted from the KS D 3507 steel pipe to establish its baseline elastoplastic properties in accordance with ASTM E8/E8M [28]. A representative stress–strain curve is presented in Figure 6, and the corresponding average mechanical properties of the three specimens are summarized in Table 5. As shown in Figure 6, the material exhibited an initial linear elastic response, followed by a smooth transition into plastic deformation without a distinct yield point, and finally reached ultimate fracture after substantial strain hardening. Accordingly, the yield strength (Fy) was determined using the 0.2% offset method specified in ASTM E8/E8M, while the ultimate tensile strength (Fu) was taken as the maximum recorded stress. As summarized in Table 5, the measured average values of Fy, Fu, and elongation (EL) were 286 MPa, 461 MPa, and 37.6%, respectively, satisfying the minimum requirements specified in KS D 3507 [26]. These results verify that the pipe material possesses sufficient strength and ductility for the subsequent structural investigation. The measured material properties were subsequently used as key input parameters for interpreting the four-point bending test results and evaluating the structural performance of the repaired steel pipes. Specifically, Fy and the corresponding yield strain were directly employed to calculate the maximum applied load (Section 3.2.1) and to evaluate the yielding behavior of the full-scale specimens (Section 3.2.2).

3.2. Structural Performance Under Four-Point Bending

3.2.1. Load–Deflection Behavior

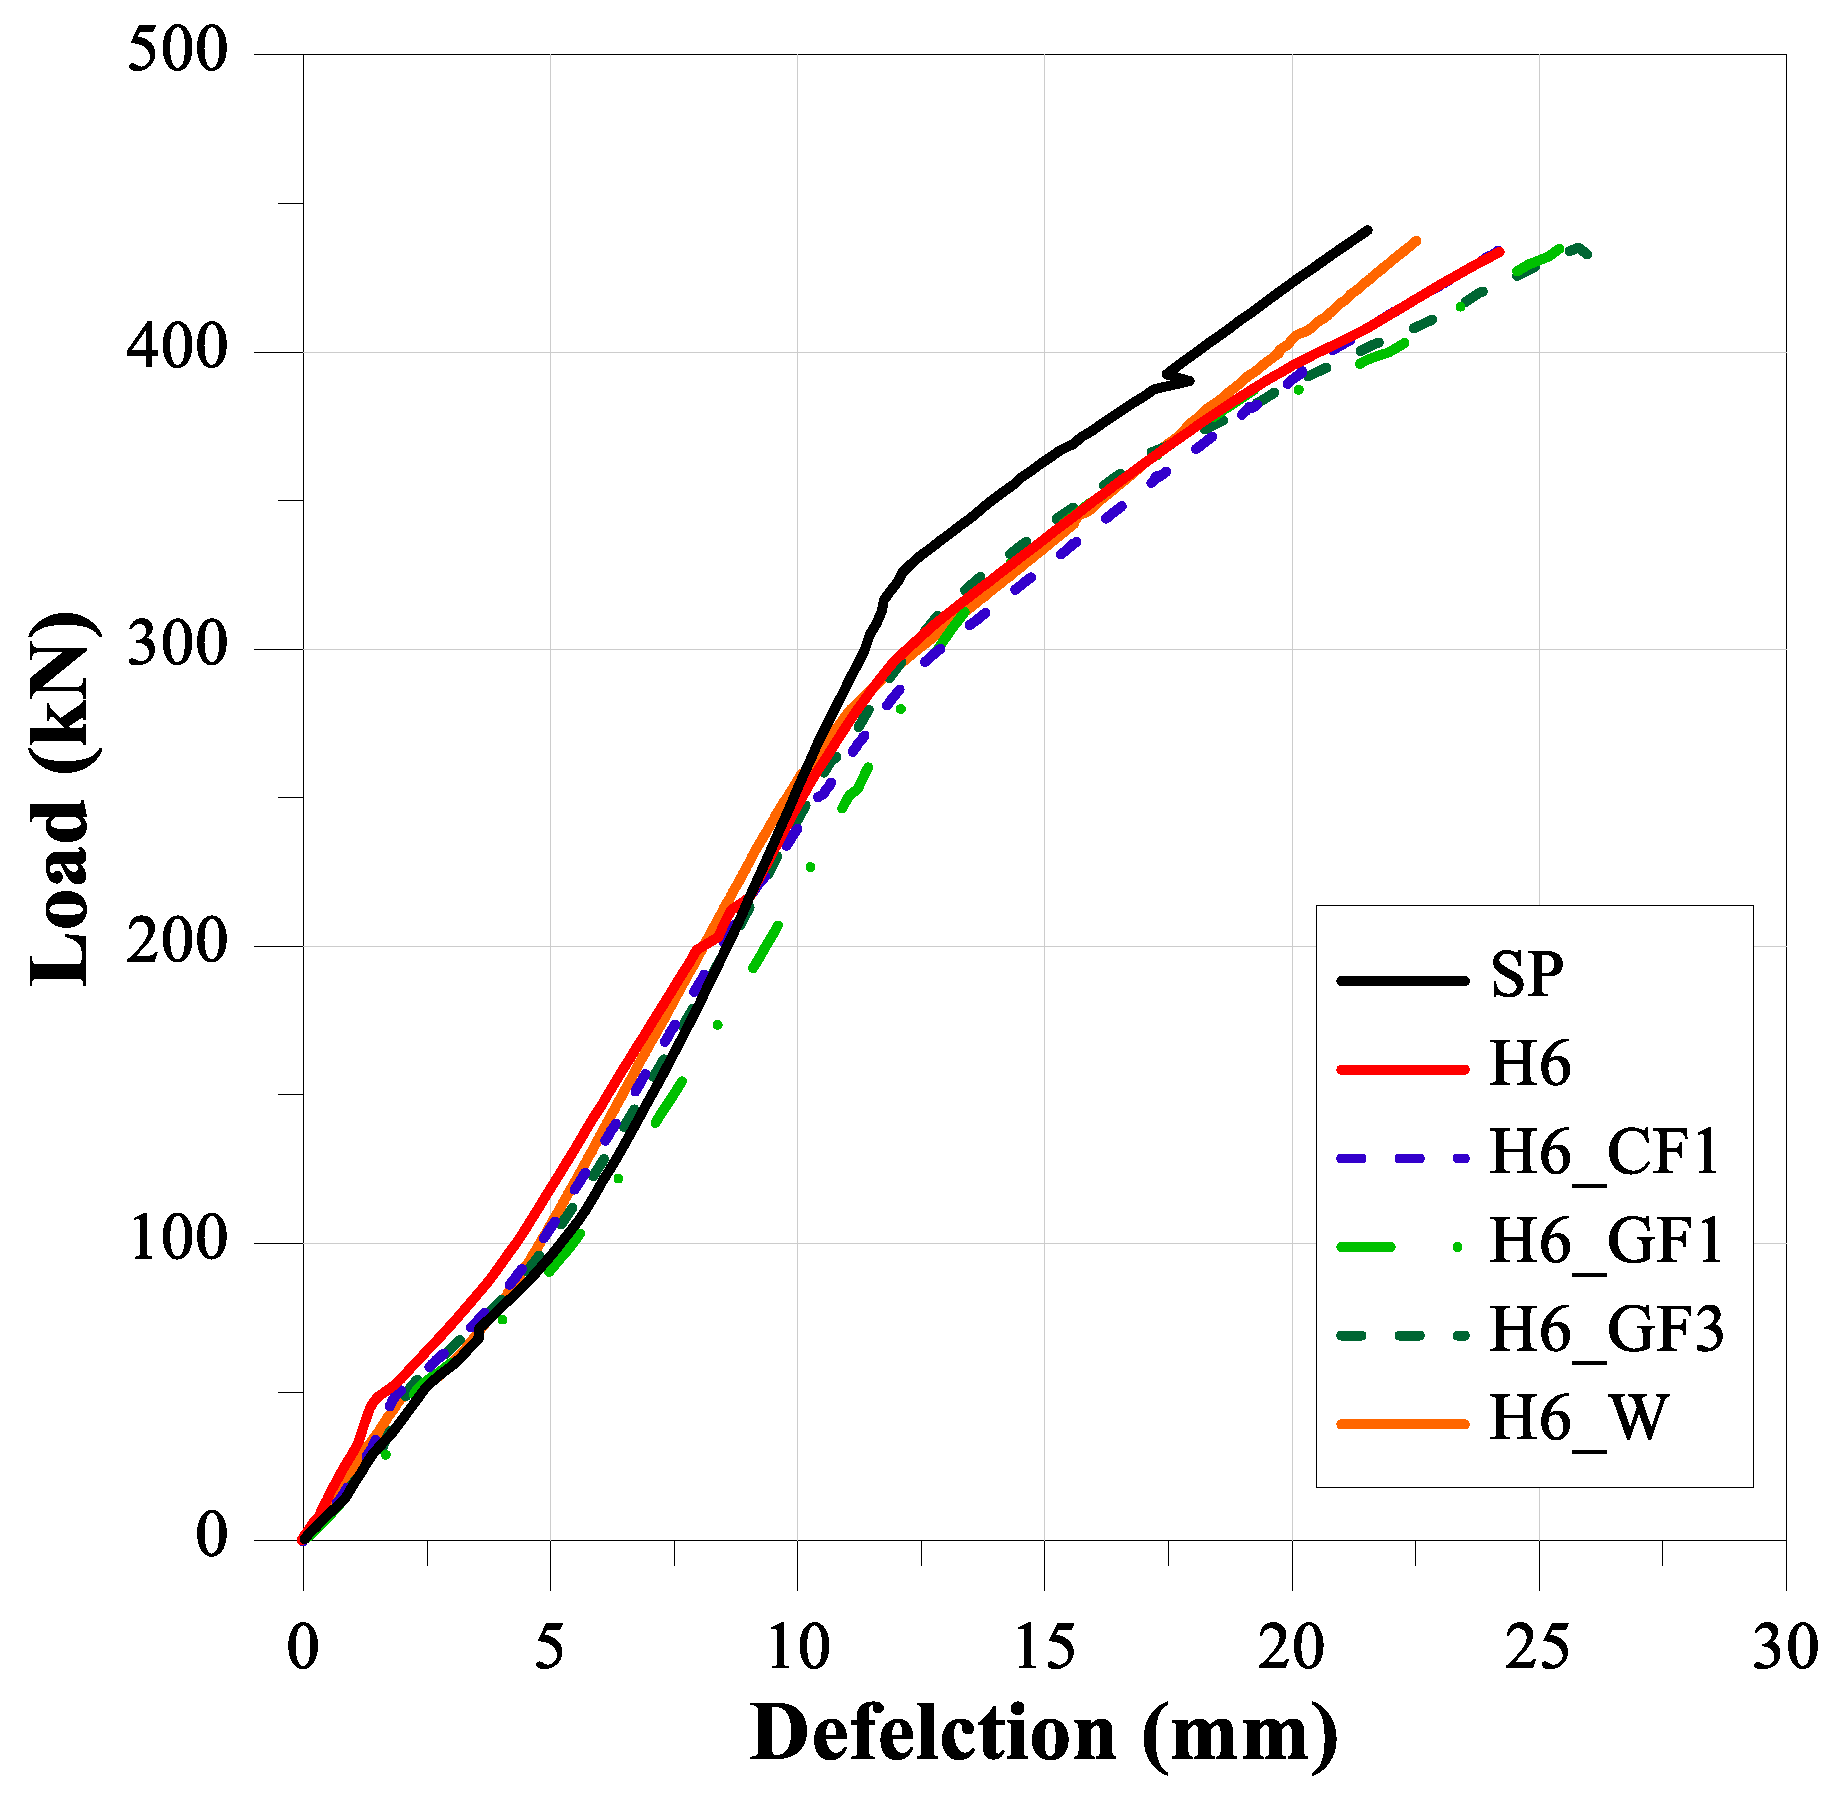
Figure 7 presents the load–deflection responses obtained from the four-point bending tests. The primary objective of these large-scale bending tests was not to drive the specimens to ultimate plastic collapse, but rather to rigorously evaluate their structural serviceability and localized load-path restoration under severe, realistic operational demands. To simulate these extreme field conditions, the maximum applied load (450 kN) was deliberately controlled to induce a bending moment slightly higher than the theoretical yield moment of the intact pipe (approximately 110% of My). This targeted loading protocol is highly justified for in-service buried pipelines. In actual field conditions, structural failure of a pipeline is typically dictated by excessive serviceability deformations—which cause joint pull-out, loss of seal, or catastrophic leakage—long before the ultimate global flexural capacity of the steel section is reached [34,35]. Furthermore, forcing the pipe into the immediate post-yield regime (110% of My) is sufficiently severe to fully mobilize the distinct stress-transfer mechanisms at the repair interfaces [36]. This specific load level effectively triggers local instability in the unreinforced defects, fully engages the interfacial shear stresses in the FRP wraps, and exposes any stiffness mismatches in the welded patches. Therefore, this controlled loading envelope accurately captures the critical transition from elastic to inelastic behavior, enabling the assessment of the repair systems under significant structural demands without introducing unrealistic global cross-sectional distortions.
Overall, the global load–deflection responses of all specimens exhibited similar trends regardless of the presence of pinhole damage or repair. All specimens initially exhibited a linear elastic response up to an applied load of approximately 50 kN. Between approximately 50 and 100 kN, a slight reduction in apparent stiffness was consistently observed before the responses returned to a stable linear elastic trend. Because this feature appeared in all specimens irrespective of the damage or repair condition, it was attributed to an experimental artifact associated with the progressive seating of the test setup rather than the intrinsic structural behavior of the steel pipes. To prevent local bearing deformation and premature cross-sectional ovalization at the support and loading points, custom solid steel internal inserts were installed at the four contact locations [37,38]. Owing to the small radial clearance between the inserts and the pipe wall, full bearing contact was established progressively during loading, resulting in a temporary evolution of the boundary conditions and load-transfer path. Once complete contact was achieved, the responses stabilized and exhibited the representative global flexural stiffness of the specimens.
Following this stabilized elastic stage, all specimens exhibited a gradual transition toward nonlinear behavior from load levels at approximately 280–320 kN. At the same deflection level, the damaged and repaired specimens (H6, H6_CF1, H6_GF1, H6_GF3, H6_W) consistently showed lower load values compared to the intact pipe (SP), indicating that introduction of the 60 mm hole resulted in a reduction in load-carrying capacity at a given deflection level regardless of the repair method applied. Despite these differences, the overall similarity of the load–deflection responses demonstrates that a highly localized defect corresponding to only 6% circumferential section loss exerts only a minor influence on the global flexural response of a 1800 mm-long pipe with an outer diameter of approximately 300 mm. This macroscopic insensitivity suggests that global deflection alone is insufficient for assessing repair effectiveness, thereby highlighting the importance of the localized interfacial strain analyses presented in Section 3.2.2.

3.2.2. Strain Responses Around the Damaged Region

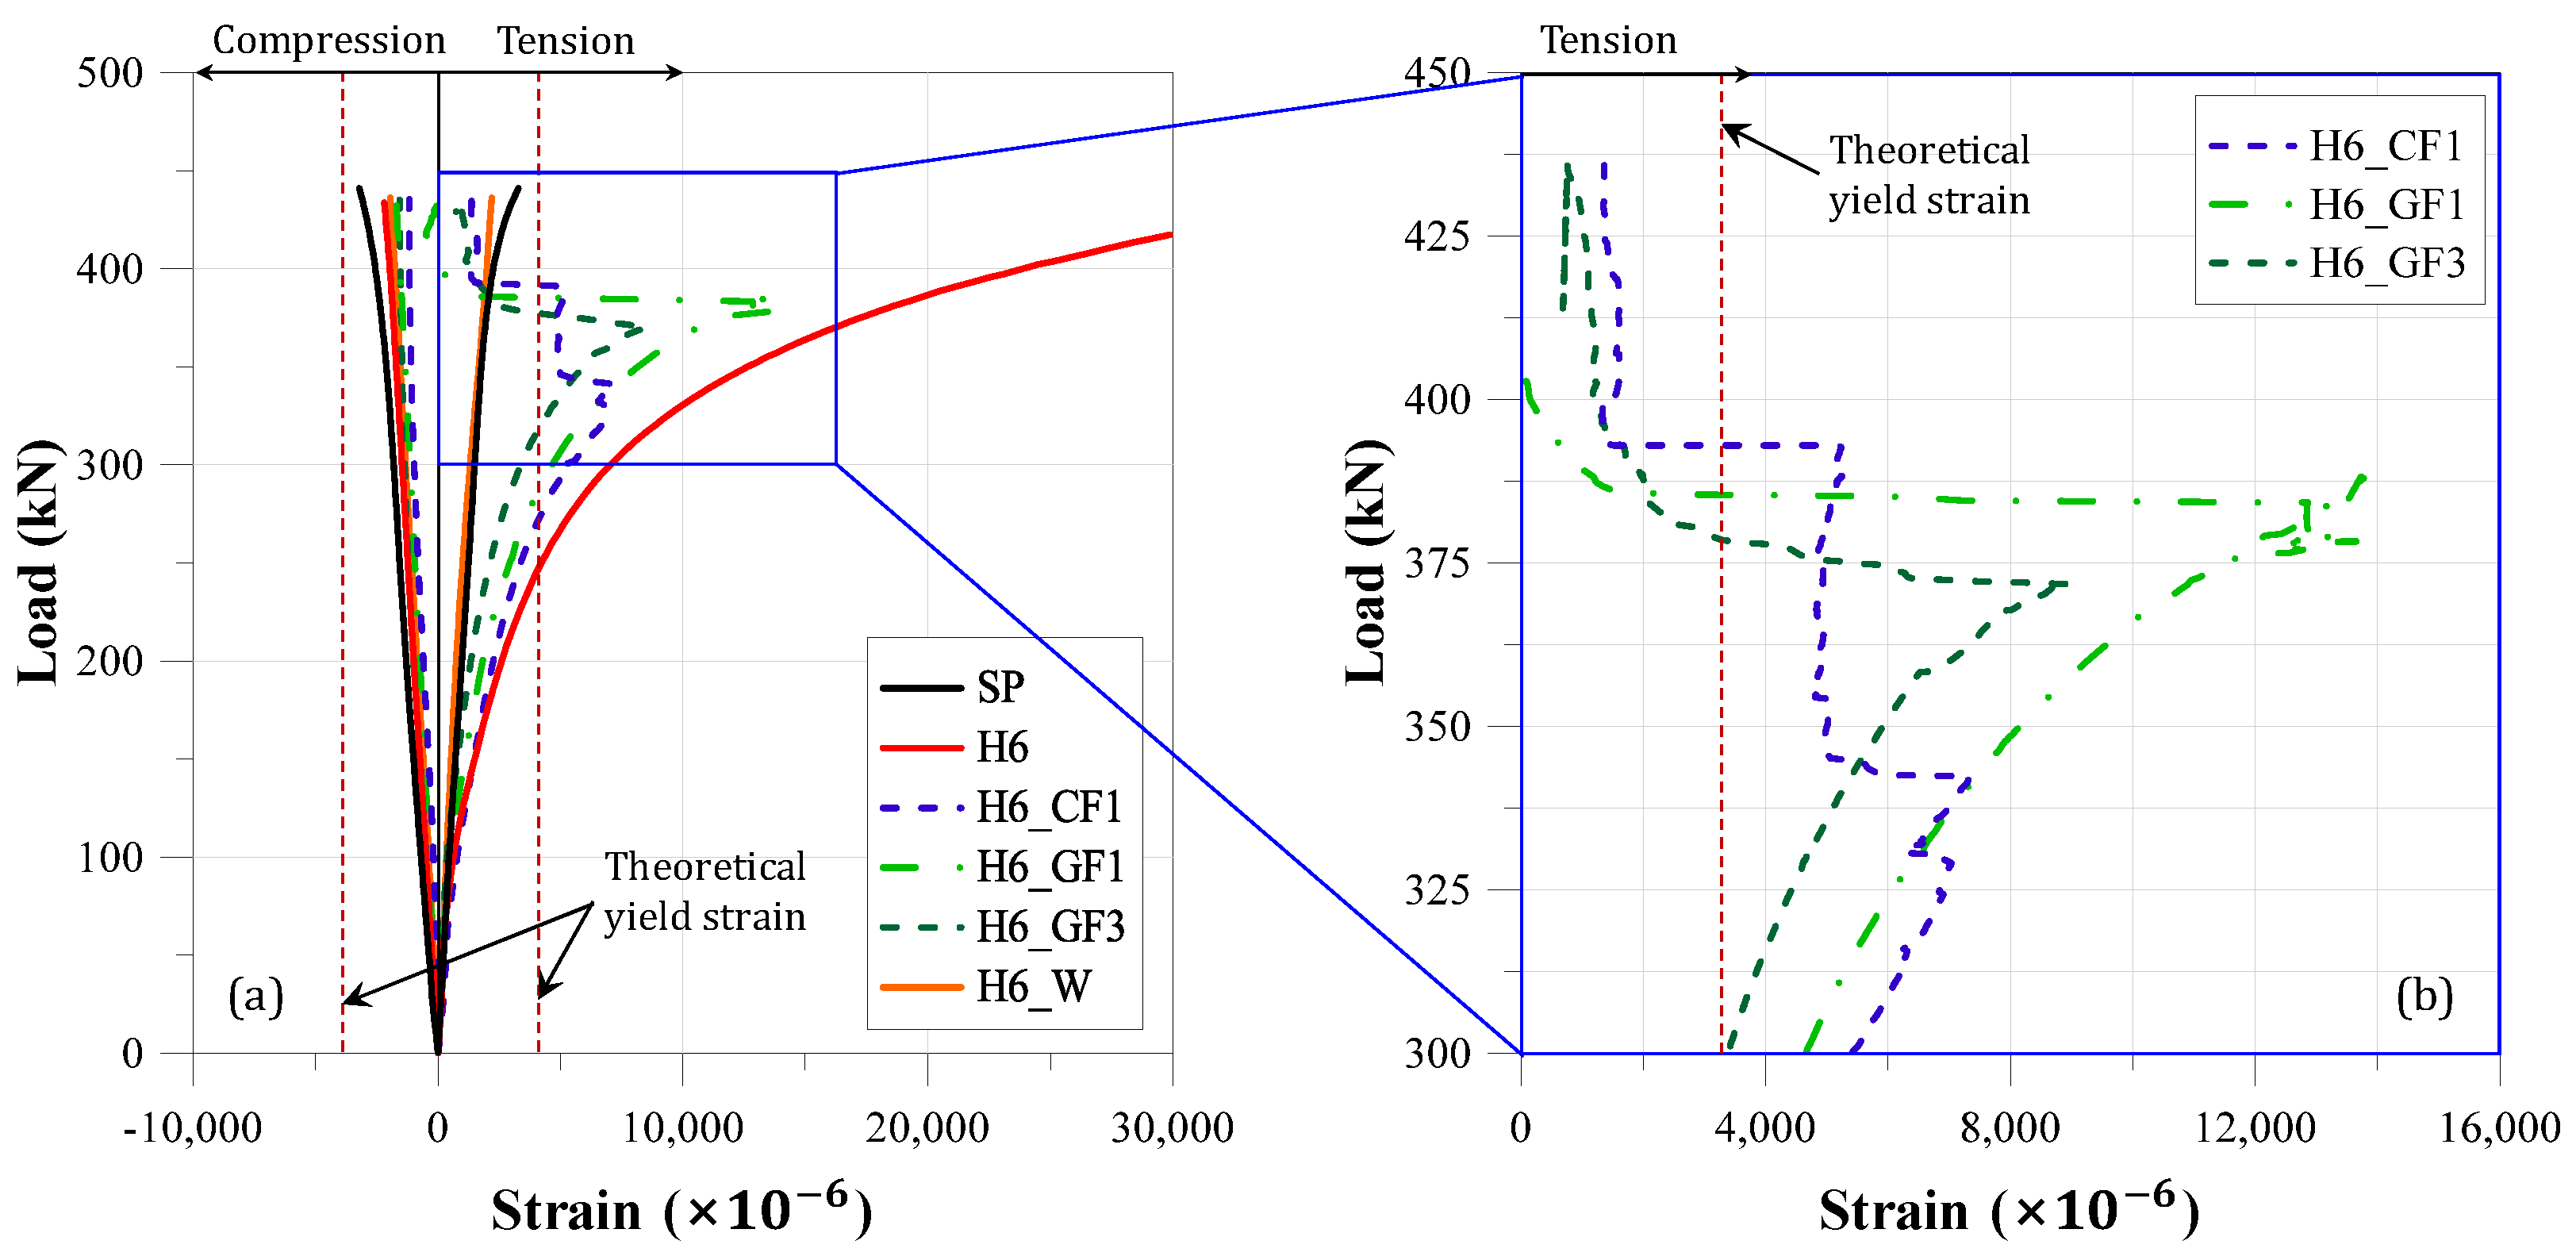
Figure 8a presents the load–strain relationships measured at the extreme compression and tension fibers of all test specimens, providing key insights into the stress redistribution and load-sharing dynamics governed by the different repair strategies. To facilitate direct comparison, compressive strain responses were plotted to the left of the origin (as negative values), while tensile strain responses were plotted to the right (as positive values). To evaluate the structural yielding state of each zone, the measured strains were benchmarked against the theoretical yield strain (εy = 3993 με, determined via the 0.2% offset method from coupon tests), which is explicitly demarcated by a red line in the plot.
On the extreme compression side (top fiber), all specimens exhibited a highly uniform and stable load–strain trend. The maximum compressive strains recorded at peak loads ranged from 1182 με to 3215 με, corresponding to only 30–80% of the yield threshold. This quantitative verification proves that failure was not governed by compression, confirming the total absence of compressive yielding or localized geometric instability (e.g., cross-sectional ovalization or local buckling) across all specimens throughout the entire loading history.
In contrast, the localized strain responses at the extreme tension fiber revealed distinct differences in the load-sharing capabilities and stress-relief mechanisms of the various repair techniques. All specimens exhibited similar strain responses up to an applied load of approximately 100 kN before significant structural resistance was mobilized. Beyond this load level, however, the unrepaired H6 specimen containing the 6% pinhole defect exhibited a rapid increase in tensile strain around the defect. The strain increased exponentially with increasing load, ultimately reaching 32,347 µε at 428 kN, which was approximately 12 times greater than that of the intact specimen (SP) at the same load level. This exponential strain divergence signifies unrestrained plastic hinging and microscopic crack propagation initiating directly from the geometric stress concentration of the pinhole, mechanistically highlighting the severe structural vulnerability caused by localized corrosion or section loss. On the other hand, the intact specimen (SP) and the welded repair specimen (H6_W) exhibited the lowest and nearly identical tensile strains throughout the loading history, and neither specimen reached the theoretical tensile yield strain even under the maximum applied load of 450 kN. This demonstrates that overlay welding effectively neutralized the stress concentration associated with the pinhole defect, thereby restoring a tensile stiffness comparable to that of the intact pipe. The FRP-repaired specimens exhibited intermediate strain levels between those of the intact and unrepaired specimens, indicating that the externally bonded composites successfully bridged the damaged region, thereby redistributing the applied load and mitigating localized stress concentrations [39,40]. Furthermore, the strain-reduction effect became more pronounced as the composite reinforcement thickness increased; however, for the same reinforcement thickness, the difference in strengthening efficacy between GFRP and CFRP was marginal.
At higher load levels above approximately 320 kN, a critical micromechanical phenomenon governing the ultimate limit state was observed in the FRP-repaired specimens. As shown in the enlarged view of Figure 8b, the strain gauges attached to the FRP surface recorded a gradual decrease in composite strain despite the continuously increasing applied load, eventually converging to values below approximately 3000 µε near 400 kN. This strain reversal is a well-established indicator of localized interfacial debonding in externally bonded FRP strengthening systems. Once the interfacial shear stress at the defect boundary exceeds the adhesive bond strength, localized separation occurs at the steel–FRP interface, disrupting the interfacial shear transfer path. This interfacial debonding mechanism aligns closely with previous studies on GFRP sleeve-repaired steel pipes [25,27], where severe flexural deformation induced a curvature mismatch between the steel substrate and the composite sleeve, initiating localized debonding along the repair boundaries and prematurely limiting composite stress transfer. Consequently, although the steel substrate continues to undergo plastic deformation under increasing load, the axial stress carried by the FRP decreases, resulting in a reduction in the measured surface strain of the composite [41].
The progression of interfacial debonding differed noticeably between the CFRP- and GFRP-repaired specimens. The CFRP-repaired specimen (H6_CF1) exhibited a reduction in strain, indicating the onset of interfacial delamination, at a lower load level than the GFRP-repaired specimens. This behavior is attributed to the pronounced stiffness mismatch between the ultra-high-modulus carbon fibers and the yielding steel substrate. In contrast, interfacial debonding in the GFRP-repaired specimens (H6_GF1 and H6_GF3) occurred at approximately 15% higher load levels. This improved debonding resistance is attributed to the relatively lower elastic modulus and greater elongation capacity of glass fibers, which permit larger interfacial shear deformations and delay catastrophic debonding, thereby promoting a more progressive damage evolution [42].

3.3. Hydrostatic Integrity and Hoop Stress Resistance

The hydrostatic pressure test results (Table 6) validate the repair methods under massive internal fluid expansion. The CFRP-repaired specimen (H6_CF1) and the welded specimen (H6_W) maintained the target pressure of 2.0 MPa throughout the test duration, resulting in a pressure retention ratio of 100%. These results demonstrate that both repair methods provided excellent sealing performance and hydrostatic integrity under the applied loading condition. In contrast, the GFRP-repaired specimens exhibited lower pressure retention ratios despite the absence of visible leakage. The final pressure of H6_GF1 decreased to 1.47 MPa, corresponding to a retention ratio of 73.5%, whereas H6_GF3 retained 1.86 MPa, corresponding to a retention ratio of 93.0%. The improved performance of H6_GF3 indicates that increasing the number of GFRP layers enhanced the ability of the repair system to maintain internal pressure. Although local radial deformation of the repaired region was not directly measured during the hydrostatic test, the observed pressure reduction in the GFRP-repaired specimens may be associated with their relatively greater radial compliance and possible localized bulging under sustained internal pressure, potentially resulting from the lower stiffness of the GFRP repair [39,43,44]. However, this interpretation was not directly verified in the present study and should therefore be regarded as a plausible explanation requiring further experimental investigation. Nevertheless, these results suggest that the stiffness and deformation characteristics of the repair system may influence its ability to maintain internal pressure over time.
Furthermore, while the current evaluation was conducted under static hydrostatic conditions, operational pipelines often encounter transient pressure surges (e.g., hydraulic impact caused by rapid valve operations). According to the literature on composite pipeline repair, circumferentially applied FRP wraps are structurally optimized to counteract such dynamic surge pressures [39,40]. The high tensile stiffness of circumferentially oriented fibers provides immediate external hoop confinement against sudden radial expansion, while the 300 mm bonded length redistributes localized impact forces away from the pinhole defect. Nevertheless, because repetitive dynamic impacts were not experimentally simulated in this static testing program, comprehensive dynamic surge and hydraulic impact testing are recommended as essential topics for future research to fully validate long-term field performance.

3.4. Accelerated Environmental Degradation (Salt Spray Test)

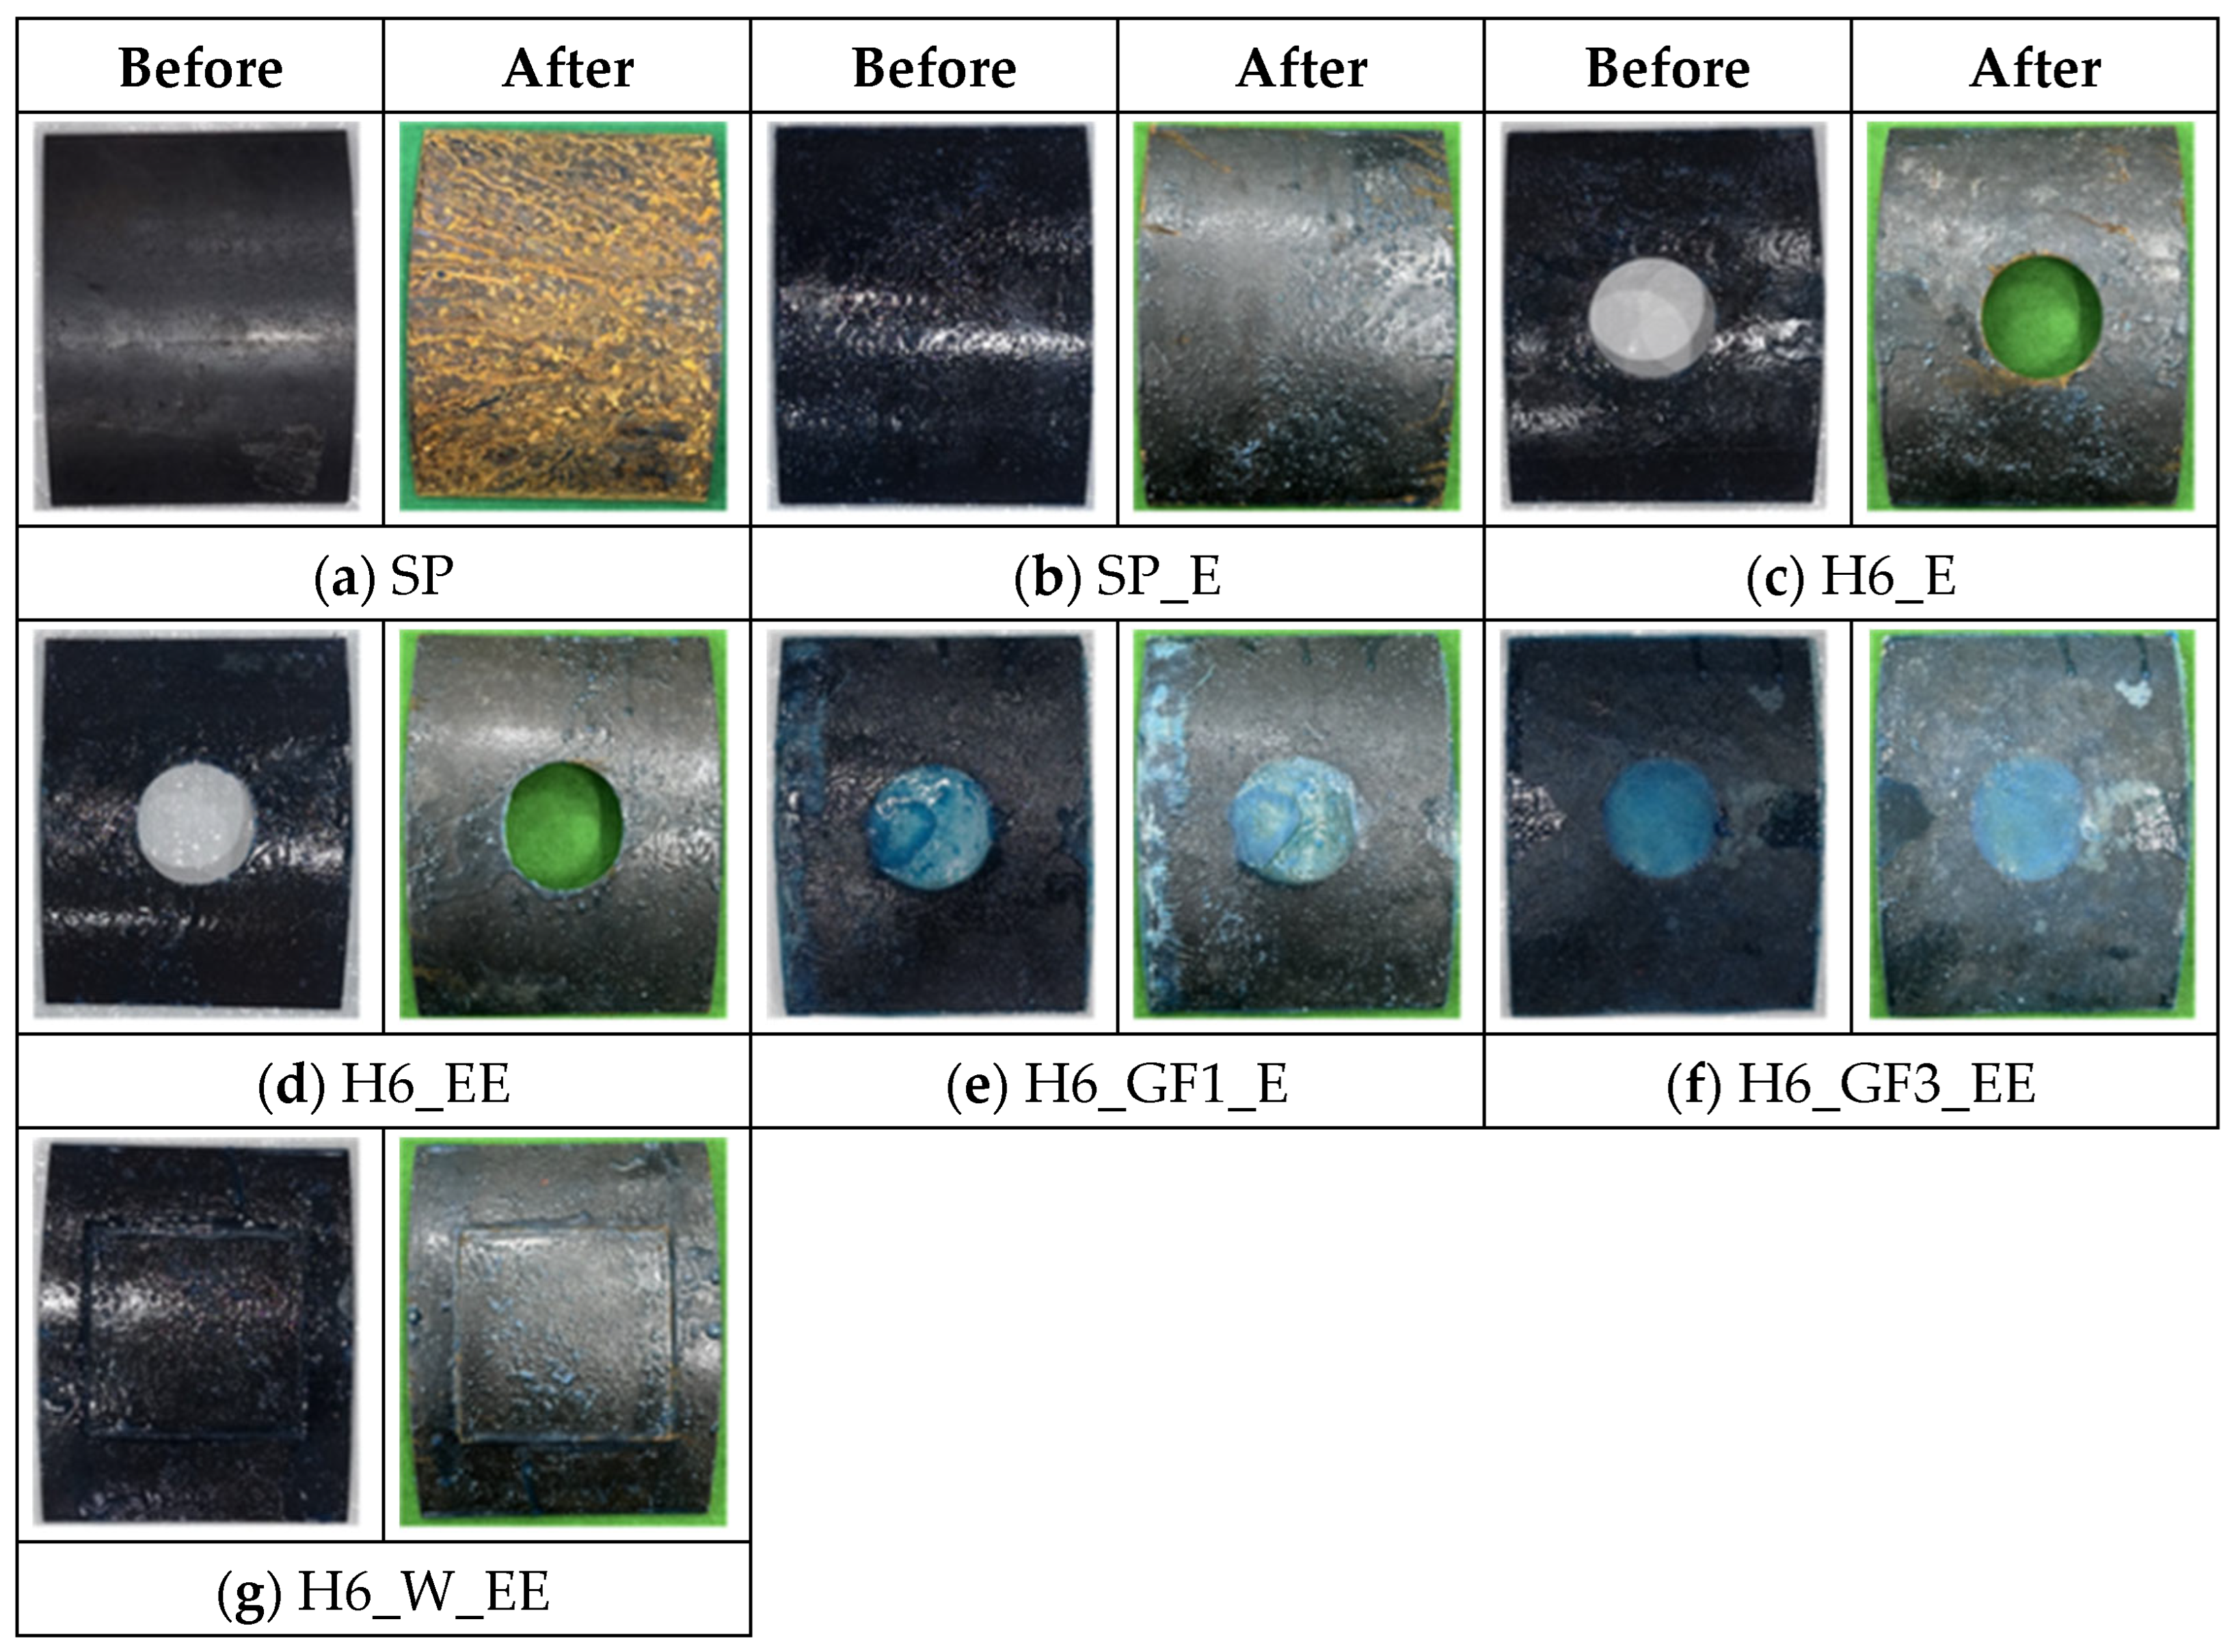
The salt spray exposure results (Figure 9 and Table 7) highlight the critical vulnerabilities and electrochemical degradation mechanisms of heterogeneous repair interfaces in aggressive chloride environments. The overall corrosion resistance was qualitatively evaluated by comparing the visual surface conditions of all specimens before and after salt spray exposure, with particular attention given to both the overall pipe surface and the localized corrosion development around the damaged hole. Based on the visual observations presented in Figure 9, the severity and extent of surface oxidation were categorized into three corrosion grades (O: General corrosion observed, ∆: Localized corrosion observed, and X: No corrosion observed), as summarized in Table 7.
As anticipated, the untreated damaged specimen (H6) exhibited severe localized corrosion around the 60 mm defect, indicating that the damaged region served as a preferential site for corrosion initiation and propagation. Such behavior is consistent with previous studies reporting that surface discontinuities facilitate the ingress of moisture and chloride ions, thereby accelerating localized corrosion [45,46,47]. While a simple epoxy coating (H6_E and H6_EE) slightly reduced general surface rusting, it completely failed to arrest localized corrosion at the defect. Surface coatings cannot bridge physical gaps, allowing electrolytes to easily bypass the barrier [48]. The welded specimen with epoxy coating (H6_W_EE) exhibited reduced corrosion severity compared with H6 and H6_EE; however, localized corrosion was still observed around the defect region after exposure. This persistent corrosion around the weld zone is primarily attributed to residual welding stresses and microstructural heterogeneity (such as grain coarsening in the heat-affected zone), which accelerate chloride ion penetration and disrupt the passive film [49]. Furthermore, the microstructural and compositional variations between the weld metal and the base steel create a galvanic potential difference. This galvanic potential difference causes the weld metal and base steel to act as an anode and a cathode, establishing localized galvanic cells that drive accelerated localized electrochemical corrosion under chloride exposure [50]. These results indicate that while the combined treatment mitigates corrosion to some extent, its protective effectiveness remains limited under chloride exposure conditions.
The best corrosion resistance was observed in the GFRP-repaired specimens (H6_GF1_EE and H6_GF3_EE). No visible corrosion was detected on either the steel surface or the defect region after testing. This behavior is attributed to the low permeability and environmental durability of the GFRP–epoxy system, which acts as an effective barrier against the ingress of moisture, oxygen, and chloride ions [51,52,53]. In addition, the complete coverage of the defect region prevented direct exposure of the steel substrate, thereby reducing the potential for localized corrosion initiation.
Overall, epoxy coating alone was insufficient to effectively suppress corrosion around the defect, whereas welding repair combined with an epoxy coating reduced the severity of corrosion to some extent. In contrast, the GFRP repair system exhibited the most effective corrosion protection among the investigated methods, suggesting its potential to enhance both the structural performance and durability of damaged agricultural steel pipelines.

4. Conclusions

This study evaluated the multi-hazard performance and failure mechanisms of full-diameter (Dp = 311.5 mm) agricultural steel pipelines repaired with CFRP and GFRP sheet wrapping as well as overlay welding. A geometric defect, corresponding to a 6% circumferential damage ratio, was introduced to simulate advanced localized pitting corrosion operating at the critical damage threshold. The repaired systems were rigorously assessed under transverse bending, internal hydrostatic pressure, and accelerated salt spray exposure. The principal conclusions are drawn as follows:
(1)
Under typical service-level flexural loading, all specimens exhibited similar global load–deflection responses regardless of the defect or repair condition. However, localized strain analyses revealed that the tensile strain around the 6% circumferential pinhole defect reached values up to 12 times greater than those of the intact pipe, promoting localized plastic deformation and microscopic crack propagation.
(2)
FRP composites effectively suppressed localized deformation, with strain-control efficacy scaling proportionally with reinforcement thickness. However, the onset of interfacial debonding—diagnosed via strain reversal—differed fundamentally between materials. Driven by a severe stiffness mismatch, the ultra-high-modulus CFRP experienced early interfacial delamination. Conversely, the GFRP system leveraged its lower modulus and elongation capacity to delay the onset of debonding by approximately 15% higher load levels.
(3)
Overlay welding emerged as the paramount structural solution, yielding load–deflection and local strain profiles nearly identical to the pristine intact pipe. By physically reconstituting the net cross-section, welding completely neutralized the stress concentrator and successfully shifted the load path away from the defect, proving its absolute structural supremacy under transverse bending.
(4)
Under a sustained internal pressure of 2.0 MPa, all interventions successfully prevented physical fluid leakage. However, notable differences in pressure-retention capacity were observed among the repair systems. The rigid welded and CFRP systems achieved 100% pressure retention throughout the test. In contrast, the single-layer GFRP specimen experienced a pressure drop (73.5% retention), which may be associated with greater radial compliance and possible local bulging at the defect region under sustained pressure, although local radial deformation was not directly measured. Tripling the GFRP layers improved the pressure-retention ratio to 93.0%, suggesting improved resistance to radial deformation.
(5)
Accelerated salt spray exposure confirmed that while welding combined with an epoxy coating mitigated overall corrosion, it offered limited localized protection. The heat-affected zones (HAZ) inherent to welding established localized galvanic cells, leading to partial degradation under chloride attack. Conversely, the GFRP systems served as an effective dielectric barrier, providing substantial protection against initial electrochemical degradation without detectable surface corrosion over the exposure duration.
(6)
Consequently, while overlay welding provides unparalleled immediate structural stiffness, adequately dimensioned GFRP systems offer a superior, balanced solution for long-term multi-hazard durability, effectively delaying interfacial failure and preventing electrochemical degradation in aging pipeline infrastructure.

Author Contributions

Conceptualization, H.-O.S. and J.-Y.L.; methodology, H.-O.S. and J.-Y.L.; formal analysis, J.C., S.K., J.-S.S. and H.-O.S.; investigation, J.C., S.K., J.-S.S., H.-O.S. and J.-Y.L.; data curation, J.C., J.-S.S. and S.K.; writing—original draft preparation, J.C., S.K., and H.-O.S.; writing—review and editing, H.-O.S. and J.-Y.L.; visualization, J.C., S.K. and J.-S.S.; supervision, H.-O.S. and J.-Y.L. project administration, H.-O.S.; funding acquisition, H.-O.S. All authors have read and agreed to the published version of the manuscript.

Funding

This work was supported by the research fund of Chungnam National University.

Institutional Review Board Statement

Not applicable.

Informed Consent Statement

Not applicable.

Data Availability Statement

The data presented in this study are available on request from the corresponding author due to a planned future patent application and the requirement for prior review and approval by the funding agency before public disclosure.

Acknowledgments

During the preparation of this work the authors used Gemini 3.1 pro and GPT-5.5 for language editing and improving the clarity of the manuscript. After using this tool/service, the author(s) reviewed and edited the content as needed and takes full responsibility for the content of the published article.

Conflicts of Interest

Author Sooho Kim was employed by the company Construction Material Test Laboratory Co., Ltd. The remaining authors declare that the research was conducted in the absence of any commercial or financial relationships that could be construed as a potential conflict of interest. The Construction Material Test Laboratory Co., Ltd. had no role in the design of the study; in the collection, analyses, or interpretation of data; in the writing of the manuscript, or in the decision to publish the results.

References

  1. Cates, W.H. Design Standards for Large-Diameter Steel Water Pipe. J. AWWA 1950, 42, 860–886. [Google Scholar] [CrossRef] [Scilit]
  2. Chen, J.; Wang, H.; Salemi, M.; Balaguru, P.N. Finite Element Analysis of Composite Repair for Damaged Steel Pipeline. Coatings 2021, 11, 301. [Google Scholar] [CrossRef] [Scilit]
  3. Ma, Y.; Li, B.; Fang, H.; Du, X.; Wang, N.; Zhai, K.; Di, D. The longitudinal mechanical behavior of steel pipes with pitting corrosion under the coupling effect of complex service loads. Int. J. Press. Vessels Pip. 2025, 214, 105423. [Google Scholar] [CrossRef] [Scilit]
  4. Dao, V.H.; Ryu, H.K.; Yoon, K.B. Leak failure at the TP316L welds of a water pipe caused by microbiologically influenced corrosion. Eng. Fail. Anal. 2021, 122, 105244. [Google Scholar] [CrossRef] [Scilit]
  5. Rajabipour, A.; Melchers, R.E. A numerical study of damage caused by combined pitting corrosion and axial stress in steel pipes. Corros. Sci. 2013, 76, 292–301. [Google Scholar] [CrossRef] [Scilit]
  6. Farh, H.M.H.; Seghier, M.E.A.B.; Taiwo, R.; Zayed, T. Analysis and ranking of corrosion causes for water pipelines: A critical review. npj Clean. Water 2023, 6, 65. [Google Scholar] [CrossRef] [Scilit]
  7. Huang, Y.; Qin, G.; Yang, M. A risk-based approach to inspection planning for pipelines considering the coupling effect of corrosion and dents. Process Saf. Environ. Prot. 2023, 180, 588–600. [Google Scholar] [CrossRef] [Scilit]
  8. Shamsuddoha, M.; Islam, M.M.; Aravinthan, T.; Manalo, A.; Lau, K.-T. Effectiveness of using fibre-reinforced polymer composites for underwater steel pipeline repairs. Compos. Struct. 2013, 100, 40–54. [Google Scholar] [CrossRef] [Scilit]
  9. Hocine, A.; Achira, F.S.K.; Habbar, G.; Levent, A.; Medjdoub, S.M.; Maizia, A.; Dhaou, M.H.; Bezazi, A. Structural integrity assessment of corroded pipelines repaired with composite materials—Literature review. Int. J. Press. Vessels Pip. 2024, 210, 105253. [Google Scholar] [CrossRef] [Scilit]
  10. Lim, K.S.; Azraai, S.; Noor, N.; Yahaya, N. An overview of corroded pipe repair techniques using composite materials. Int. J. Mater. Metall. Eng. 2016, 10, 19–25. [Google Scholar]
  11. Lukács, J.; Koncsik, Z.; Chován, P. Integrity increasing of damaged transporting pipelines using fiber reinforced polymer composite wrap systems. Eng. Fail. Anal. 2022, 137, 106284. [Google Scholar] [CrossRef] [Scilit]
  12. Mahdi, E.; Eltai, E. Development of cost-effective composite repair system for oil/gas pipelines. Compos. Struct. 2018, 202, 802–806. [Google Scholar] [CrossRef] [Scilit]
  13. Muda, M.F.; Hashim, M.H.M.; Kamarudin, M.K.; Mohd, M.H.; Tafsirojjaman, T.; Rahman, M.A.; Paik, J.K. Burst pressure strength of corroded subsea pipelines repaired with composite fiber-reinforced polymer patches. Eng. Fail. Anal. 2022, 136, 106204. [Google Scholar] [CrossRef] [Scilit]
  14. Ghimire, A.; Aslani, F.; Walker, L. Advances in composite repair strategies for structural damage in aging steel infrastructure: A review. Structures 2026, 90, 112387. [Google Scholar] [CrossRef] [Scilit]
  15. Elchalakani, M.; Karrech, A.; Basarir, H.; Hassanein, M.F.; Fawzia, S. CFRP strengthening and rehabilitation of corroded steel pipelines under direct indentation. Thin-Walled Struct. 2017, 119, 510–521. [Google Scholar] [CrossRef] [Scilit]
  16. Brahim, A.O.; Belaidi, I.; Khatir, S.; Le Thanh, C.; Mirjalili, S.; Wahab, M.A. Strength prediction of a steel pipe having a hemi-ellipsoidal corrosion defect repaired by GFRP composite patch using artificial neural network. Compos. Struct. 2023, 304, 116299. [Google Scholar] [CrossRef] [Scilit]
  17. Li, A.; Wang, H.; Li, H.; Kong, D.; Xu, S. Stress Concentration Analysis of the Corroded Steel Plate Strengthened with Carbon Fiber Reinforced Polymer (CFRP) Plates. Polymers 2022, 14, 3845. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  18. Tafsirojjaman, T.; Fawzia, S.; Thambiratnam, D.P.; Wirth, N. Performance of FRP strengthened full-scale simply-supported circular hollow steel members under monotonic and large-displacement cyclic loading. Eng. Struct. 2021, 242, 112522. [Google Scholar] [CrossRef] [Scilit]
  19. Li, M.; She, Y.; He, J.; Zhou, L.; Pan, X. Research on multimodal damage monitoring of CFRP- steel pipe composite structures under three point bending loads. Constr. Build. Mater. 2025, 489, 142304. [Google Scholar] [CrossRef] [Scilit]
  20. Flaifel, T.R.; Mosalmani, R.; Al-Sabur, R.; Shishesaz, M. Experimental investigation of through-wall hole geometry on pressure resistance in steel pipelines repaired with composite materials. Discov. Mater. 2025, 5, 212. [Google Scholar] [CrossRef] [Scilit]
  21. Bekgöz, M.H.; Turan, F. Experimental investigation of layer number, fiber architecture, orientation, and areal density on the mechanical behavior and failure mechanism of FRP adhesive joints. J. Adhes. Sci. Technol. 2025, 39, 3271–3292. [Google Scholar] [CrossRef] [Scilit]
  22. Romanowicz, P.; Szybiński, B.; Wygoda, M. Fracture Mechanism of Adhesive Layers in Fatigue-Loaded Steel Structures Reinforced by the CFRP Overlays. Appl. Sci. 2025, 15, 3435. [Google Scholar] [CrossRef] [Scilit]
  23. Yu, Y.; Li, D.; He, L.; Tam, L.-H.; Wang, Z.; Wu, C. Corrosion-Induced Degradation Mechanisms and Bond–Slip Relationship of CFRP–Steel-Bonded Interfaces. Materials 2026, 19, 511. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  24. Heggab, A.; El Aghoury, I.M.; El Nemr, A. Numerical analysis for failure estimation of compositely rehabilitated corroded pipes under operational and ultimate states. Eng. Fail. Anal. 2024, 163, 108533. [Google Scholar] [CrossRef] [Scilit]
  25. Kim, S. Evaluation of the Applicability of Various Repair Methods for Aging Agricultural Steel Pipes. Master’s Thesis, Chungnam National University, Daejeon, Republic of Korea, 2025. [Google Scholar] [CrossRef]
  26. KS D 3507:2025; Carbon Steel Pipes for Ordinary Piping. Korean Standards Association: Seoul, Republic of Korea, 2025.
  27. Lee, J.-H.; Kim, S.; Park, C.-G.; Shin, H.-O.; Banthia, N. Load-Dependent Performance of Repair Techniques for Corrosion-Induced Pinhole Defects in Agricultural Pipelines. Materials 2026, 19, 3182. [Google Scholar] [CrossRef] [Scilit]
  28. ASTM E8/E8M-22; Standard Test Methods for Tension Testing of Metallic Materials. ASTM International: West Conshohocken, PA, USA, 2022.
  29. Westra, L.; Breaux, M.W.; Richard, R., Jr.; Wilson, C.D. Hydrostatic Pressure Testing System and Method. US8731849B2, 20 May 2014. [Google Scholar]
  30. ASTM B117-26; Standard Practice for Operating Salt Spray (Fog) Apparatus. ASTM International: West Conshohocken, PA, USA, 2026.
  31. Uvida, M.C.; Almeida, A.D.A.; Pulcinelli, S.H.; Santilli, C.V.; Hammer, P. Structural properties of epoxy–silica barrier coatings for corrosion protection of reinforcing steel. Polymers 2022, 14, 3474. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  32. Lu, Z.; Xie, J.-H.; Zhang, H.; Li, J. Long-term durability of basalt fiber-reinforced polymer (BFRP) sheets and the epoxy resin matrix under a wet–dry cyclic condition in a chloride-containing environment. Polymers 2017, 9, 652. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  33. Wijewickrama, L.; Jeewantha, J.; Perera, G.; Alajarmeh, O.; Epaarachchi, J. Fiber-reinforced composites used in the manufacture of marine decks: A review. Polymers 2025, 17, 2345. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  34. Qin, X.; Wang, Y.; Fu, C. Joint Kinematics and Sealing Capacity Assessment of Ductile Iron Pipes under Abrupt Transverse Ground Movements. Can. Geotech. J. 2021, 59, 342–358. [Google Scholar] [CrossRef] [Scilit]
  35. Wham, B.P.; Argyrou, C.; O’Rourke, T.D. Jointed pipeline response to tunneling-induced ground deformation. Can. Geotech. J. 2016, 53, 1794–1806. [Google Scholar] [CrossRef] [Scilit]
  36. Kiriella, S.; Manalo, A.; Tien, C.M.T.; Ahmadi, H.; Wham, B.P.; Salah, A.; Tafsirojjaman, T.; Karunasena, W.; Dixon, P.; O’Rourke, T.D. Lateral deformation behaviour of structural internal replacement pipe repair systems. Compos. Struct. 2023, 319, 117144. [Google Scholar] [CrossRef] [Scilit]
  37. Yang, Z.; Meng, X.; Walport, F.; Gardner, L. Flexural capacity and local buckling half-wavelength of high strength steel tubular beams under moment gradients: An experimental study. Thin-Walled Struct. 2024, 195, 111420. [Google Scholar] [CrossRef] [Scilit]
  38. Seong, M.; Kang, S.; Kim, J. Flexural Performance Evaluation of Steel Pipe Considering Material Property Change by Pipe-Forming. J. Korean Soc. Steel Constr. 2022, 34, 319–329. [Google Scholar] [CrossRef] [Scilit]
  39. Reis, J.; Costa, A.R.; Da Costa Mattos, H.S. Repair of damage in pipes using bonded gfrp patches. Compos. Struct. 2022, 295, 115875. [Google Scholar] [CrossRef] [Scilit]
  40. Shi, J.; Wang, W.; Wei, W.; Jia, B. Calculation model for bearing capacity of steel-CFRP composite pipeline under internal pressure. Heliyon 2024, 10, e27238. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  41. Maalej, M.; Leong, K.S. Effect of beam size and FRP thickness on interfacial shear stress concentration and failure mode of FRP-strengthened beams. Compos. Sci. Technol. 2005, 65, 1148–1158. [Google Scholar] [CrossRef] [Scilit]
  42. Atakok, G.; Yoldas, D.M. Comparison of GFRP (Glass Fiber-Reinforced Polymer) and CFRP (Carbon Fiber-Reinforced Polymer) Composite Adhesive-Bonded Single-Lap Joints Used in Marine Environments. Sustainability 2024, 16, 11105. [Google Scholar] [CrossRef] [Scilit]
  43. Chen, R.; Qiu, J.; Liu, B.; Ren, G. Ultimate Failure of Defective Pipelines Reinforced with Composite Repair Systems. J. Fail. Anal. Prev. 2019, 19, 581–589. [Google Scholar] [CrossRef] [Scilit]
  44. Lim, K.S.; Azraai, S.N.A.; Yahaya, N.; Noor, N.; Zardasti, L.; Kim, J. Behaviour of steel pipelines with composite repairs analysed using experimental and numerical approaches. Thin-Walled Struct. 2019, 139, 321–333. [Google Scholar] [CrossRef] [Scilit]
  45. Song, G.-L.; Feng, Z. Modification, Degradation and Evaluation of a Few Organic Coatings for Some Marine Applications. Corros. Mater. Degrad. 2020, 1, 408–442. [Google Scholar]
  46. Koleva, D.A. An Innovative Approach to Control Steel Reinforcement Corrosion by Self-Healing. Materials 2018, 11, 309. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  47. Zhao, X.; Munroe, P.; Habibi, D.; Xie, Z. Roles of compressive residual stress in enhancing the corrosion resistance of nano nitride composite coatings on steel. J. Asian Ceram. Soc. 2013, 1, 86–94. [Google Scholar] [CrossRef] [Scilit]
  48. Fan, L.; Reis, S.T.; Chen, G.; Koenigstein, M.L. Corrosion Resistance of Pipeline Steel with Damaged Enamel Coating and Cathodic Protection. Coatings 2018, 8, 185. [Google Scholar] [CrossRef] [Scilit]
  49. Peng, C.; Mei, Q.; Han, J.; Han, E.; Ke, W. Microstructure and corrosion behavior of the heat affected zone of a stainless steel 308L-316L weld joint. J. Mater. Sci. Technol. 2018, 34, 1819–1828. [Google Scholar] [CrossRef] [Scilit]
  50. Maurya, A.; Pandey, S.; Chhibber, R.; Fydrych, D.; Pandey, C. Corrosion performance of super duplex stainless steel and pipeline steel dissimilar welded joints: A comprehensive investigation for marine structures. Int. J. Adv. Manuf. Technol. 2024, 135, 1009–1033. [Google Scholar] [CrossRef] [Scilit]
  51. Khoe, C.; Sen, R.; Venkat, R.B. Oxygen Permeability of Fiber-Reinforced Polymers. J. Compos. Constr. 2011, 15, 513–521. [Google Scholar] [CrossRef] [Scilit]
  52. Alabtah, F.G.; Mahdi, E.; Khraisheh, M. External Corrosion Behavior of Steel/GFRP Composite Pipes in Harsh Conditions. Materials 2021, 14, 6501. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  53. Alabtah, F.G.; Mahdi, E.; Eliyan, F.F.; Eltai, E.; Khraisheh, M. Towards the Development of Novel Hybrid Composite Steel Pipes: Electrochemical Evaluation of Fiber-Reinforced Polymer Layered Steel against Corrosion. Polymers 2021, 13, 3805. [Google Scholar] [CrossRef] [Scilit] [PubMed]
Figure 1. Schematic illustration of the steel pipe specimen, artificial pinhole damage, and repair methods.
Applsci 16 07761 g001
Figure 2. Extracted coupon specimens and test set-up for the tensile test.
Applsci 16 07761 g002
Figure 3. Four-point bending test details: (a) overall test set-up; (b) support and loading points with internal steel inserts.
Applsci 16 07761 g003
Figure 4. Hydrostatic pressure test set-up.
Applsci 16 07761 g004
Figure 5. Salt spray test set-up. (a) experimental equipment. (b) details of workroom.
Applsci 16 07761 g005
Figure 6. Typical stress–strain curve of the extracted coupon specimens (specimen #1).
Applsci 16 07761 g006
Figure 7. Load–deflection curve for four-point bending test.
Applsci 16 07761 g007
Figure 8. Load-strain responses: (a) all specimens; (b) FRP repaired specimens at high load level (>300 kN).
Applsci 16 07761 g008
Figure 9. Salt spray test results before and after exposure.
Applsci 16 07761 g009
Table 1. Test variables.
VariablesPinhole DamageRepair MethodDescription
SPNoneNoneIntact control specimen
H6dh = 60 mm (6%)NoneDamaged, unrepaired
H6_CF1CFRP Sheet-1 layerDamaged, 1 layer of CFRP sheet repair
H6_GF1GFRP Sheet-1 layerDamaged, 1 layer of GFRP sheet repair
H6_GF3GFRP Sheet-3 layersDamaged, 3 layers of GFRP sheet repair
H6_WOverlay weldingDamaged, patch welding repair
Note: Specimen counts per variable were n = 1 for the four-point bending tests (due to practical constraints of full-scale testing), n = 2 for the hydrostatic pressure tests, and n = 2 for the salt spray exposure tests.
Table 2. Mechanical properties of the FRP sheets.
PropertiesCFRP SheetGFRP Sheet
Elastic modulus (GPa)21040
Poisson’s ratio0.20.2
Shear modulus (GPa)76
Mass density (g/cm3)1.72
Tensile strength (MPa)21001000
Compressive strength (MPa)1000600
Yield strengthIt generally fails at the maximum tensile or compressive strength
Thermal expansion coefficientAlong the fiber direction: approx. 0.5–1.5 × 10⁻⁶/°C
Transverse to the fiber direction: approx. 30–50 × 10−6/°C
Thermal conductivity (W/m∙k)100.3
Specific heat (J/kg∙K)9001000
Material damping ratio0.020.02
Thickness (mm)2 mm/layer2 mm/layer
Table 3. Mechanical properties of the epoxy resin and primer.
PropertiesPrimerEpoxy Resin
Application temperature (°C)15–2515–25
Pot life (min)4040
Surface drying time (h/20 °C)Within 11 hWithin 11 h
Mixing ratio by weight (base:hardener)2:12:1
Viscosity (cps/20 °C)13005000
Tensile strength (MPa)5050
Flexural strength (MPa)-40
Compressive strength (MPa)-70
Compressive modulus (MPa) 1500
Tensile shear bond strength (metal:metal) (MPa)-10
Lap shear strength (CF:CF sheet) (MPa)-39
Table 4. Test variables for the salt spray test.
Variables Pinhole DamageRepair MethodEpoxy Resin Coating
Pipe SurfacePinhole Perimeter
SPNoneNoneX- *
SP_Edh = 60 mm (6%)NoneO- *
H6_ENoneOX
H6_EENoneOO
H6_GF1_EEGFRP Sheet-1 layerOO
H6_GF3_EEGFRP Sheet-3 layersOO
H6_W_EEOverlay weldingOO
* Specimens without pinhole.
Table 5. Mechanical properties of the steel pipe.
PropertiesYield Strength *
(Fy, MPa)
Ultimate Strength
(Fu, MPa)
Elongation
(EL, %)
Measured286 (10.5) **461 (27.8) **37.6 (1.5) **
Mill test certificate27545239.0
KS requirement≥200≥340≥30.0
* 0.2% offset value, ** (): Standard deviations (S.D.) are presented in parentheses.
Table 6. Summary of hydrostatic pressure test results.
SpecimensInitial Pressure
(MPa)
Final Pressure
(MPa)
Pressure Retention Ratio (%)Leakage
H6_CF12.002.00100None
H6_GF12.001.4773.5None
H6_GF32.001.8693.0None
H6_W2.002.00100None
Table 7. Corrosion observations before and after salt spray testing.
SpecimensCorrosion Observation Before TestingCorrosion Observation After Testing
Pipe SurfacePinhole Perimeter
SPXO-
SP_EX-
H6_EXO
H6_EEX
H6_GF1_EEX
H6_GF3_EEXXX
H6_W_EEXXX
Note: O = General corrosion (widespread oxidation and heavy surface rust observed); ∆ = Localized corrosion (slight surface discoloration or minor localized rust observed); X = No corrosion (no visible oxidation or surface rust observed).
Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content.