Review

Hybrid Modular Mining Structures: A Review of Design Actions and Prefabricated Connection Solutions


1
Centre for Infrastructural Monitoring and Protection, School of Civil and Mechanical Engineering, Curtin University, Bentley, WA 6102, Australia
2
Earthquake Engineering Research & Test Center, Guangzhou University, Guangzhou 510006, China
*
Author to whom correspondence should be addressed.
Buildings 2026, 16(9), 1675; https://doi.org/10.3390/buildings16091675
Submission received: 28 January 2026 / Revised: 7 April 2026 / Accepted: 19 April 2026 / Published: 24 April 2026
(This article belongs to the Special Issue Innovative Design and Optimization of Steel Structures)

Abstract

Fully volumetric modular mining structures offer a partial solution to achieving sustainable construction at remote mine sites. Significant logistical challenges arise during road and sea transportation, depending on the size of the prefabricated modules and the remoteness of the site. As an alternative, hybrid modular mining structures comprising various non-volumetric prefabricated components of transportable size, assembled on-site to form complete structures, have previously been proposed. To facilitate hybrid modular structures in the mining industry, the paper reviews the design actions to which mining structures are subjected and evaluates the corresponding structural responses. It also examines existing connections that may be suitable for the hybrid module structures, assessing their effectiveness and safety in connecting prefabricated structural components. Finally, key requirements for connection design are identified to facilitate hybrid assembly.

1. Introduction

In the mining industry, infrastructure is broadly categorised into process and non-process infrastructure. Mining structures are classified as process infrastructure when they directly involve the extraction and processing of minerals. Mining structures that are not involved in the ore extraction process but are essential to the operation of the mine are referred to as non-process infrastructure. The work presented in this paper focuses on process infrastructure, which is primarily defined as structures involved in the extraction process, as illustrated in Figure 1. The structural steelwork in these structures was historically fabricated in regional centres and transported as individual or “stick” components to the mine site. Each stick component requires human effort and craneage in order to assemble the stick-built structures, resulting in substantial site work hours for structure erection. The rising costs and labour shortage in Australia are driving an increased focus on improving productivity and reducing labour-intensive tasks on the worksite, especially at remote mining locations, where the work could be performed in regional areas or in low-cost overseas centres. Kreppold et al. [1] reviewed the benefits of prefabricated volumetric structures in terms of safety, productivity, quality, schedule, cost and sustainability, as well as the challenges involved. Fabrication and assembly of structural steel are most cost-effective in a low-cost environment, enabling the delivery of complete modular structures to remote mining locations.
The construction industry generally faces challenges regarding emissions, efficiency, sustainability and safety [2,3,4,5,6,7,8,9,10,11]. The deficiencies also extend to construction at remote mining sites, with additional factors such as cost, wastefulness [12], and socioeconomic impacts [13,14,15,16,17,18]. As the world is seeking sustainability and carbon neutrality, the need for critical minerals is increasing dramatically [19]. With this growth in demand for critical minerals, there is an increasing spotlight on the efficiencies of those producing the minerals [20]. Volumetric prefabrication is credited with providing a more sustainable and efficient approach for construction, generally [2,3,5,6,7,8,10,11,21], and reducing the negative impact on remote locations. The assembly of two-dimensional prefabricated component structures is also considered efficient and less wasteful [22] than conventional construction methods.
Mine sites are frequently distant from the coast and tend to be concentrated in remote parts of Australia [23,24]. Such locations preclude the use of, or pose logistical challenges for, transporting large prefabricated structures from coastal wharfs to remote mine sites, and are therefore unsuitable for full volumetric construction. These locations require an efficient, sustainable alternative that offers many of the benefits of volumetric construction. Prefabricated components of transportable size, consisting of end frames and panels, that can be site assembled, are herein defined as hybrid modular structures and are preferred over stick components if volumetric prefabrication is unsuitable due to size constraints. Prefabricated end frames and panels are problematic as they cannot be safely joined using current beam–column connections. An alternative connection style is required to overcome this problem. Beam–column connections that eliminate the need for a human to be under or on a suspended load are required. The ideal solution allows prefabricated components to be safely joined, supported and structurally stable, fitting together without close human involvement at the interface.
Mining structures are subjected to operational loads that are not present in conventional structures, resulting in actions and combinations not anticipated in typical loading codes and standards. It is therefore fitting to assess the various hazards and loads to which both prefabricated and conventional mining structures are subjected, and the structural responses that result. Armed with an understanding of the hazard and expected response required for fit-for-purpose mining structures, a review of the various beam–column connection details is performed in this study. This review focuses on existing beam–column connections, reviewing their suitability for adaptation for use within the mining industry and for joining prefabricated end frames and panels into hybrid modular structures.
In summary, this review paper provides an overview of the loading conditions imposed on mining structures, considering gravity and environmental, transient, operational, lifting, and transport loads. Next, the review considers the response of mining structures to these various types of loading, and then discusses the desired characteristics of beam–column connections if used to join prefabricated components into hybrid modular structures. With the desired characteristics for joining prefabricated components in mind, a review of field connection techniques applicable to on-site assembly is undertaken, and future perspectives are identified. This review adopts an analytical, criteria-based synthesis to identify research gaps and limitations relevant to hybrid modular mining structures.

2. Overview of Loading Conditions

Mining structures are unique in that they are not only subjected to hazards typical of conventional structures; they are also subjected to a variety of additional transient loads due to the nature of their intended ore processing purpose during the operation. Although various design standards address specific elements of mining infrastructure—such as underground mining structures and mine shafts—no comprehensive, unified standard currently governs the overall structural design of mining facilities. Consequently, mining steelwork is generally engineered in accordance with general structural steel design codes and tailored project requirements, rather than a consistent mining-specific framework. The design of volumetric and prefabricated structures also differs from conventional construction, as additional loading conditions arise from lifting, transportation, handling, and placement requirements. These additional loading conditions necessitate greater engineering input [25]. Therefore, these types of mining structures are unique in terms of the design loads to which they are subjected. The role of structural engineering, amongst other things, is to, within an accepted risk, ensure that a structure can resist the loads and hazards to which it is exposed throughout its life. Any loading conditions imposed on prefabricated structures must be understood, and the structures must be engineered to ensure appropriate and acceptable structural responses.
Whilst a process structure is subject to multiple hazards, these are variously grouped into natural, anthropogenic, and technological hazards [26,27,28]. From a structural engineering perspective, these hazards can be divided into two categories: those that induce loads and those that affect structural durability and long-term performance. The art of rigorous load assessment is understanding the various combinations and proportions in which these hazards present themselves. Whilst the various hazards can be described as concurrent, cascading or independent [28,29], the combination of the hazards producing loads has largely been codified [30,31,32] for non-process-type structures. In Australia, the codification of the combination of hazards [30] covers the structure’s ultimate strength and serviceability requirements. The codes also require structural and material durability to ensure the structure can fulfil its intended design life. The loading codes are written with general buildings in mind and are not bespoke to mining structures or volumetric prefabrication. Whilst the legislated loading requirements must be complied with, there are additional considerations beyond those outlined in the national structure loading standards, as stated in [33]. The Australian loading codes do not cover all the loads and combinations to which a mining structure is subject. Bespoke design load combinations are frequently developed on a project-specific basis, encompassing the minimum requirements of the Australian Standards, likely additional load combinations, and in-service and operating loads [34]. Risk assessments are conducted by project insurers, financiers, and owners, and load probabilities are adjusted based on the project’s appetite for risk. It is common to assign a 50-year design life to short-duration projects for non-structural reasons.
Load-induced hazards in prefabrication in the mining industry can be grouped into four main categories. These categories include gravity-induced load, environmental-induced load, transient and operational loads, and lifting and transportation loads for volumetric prefabrication. As this study focuses on hybrid modular structures, it is appropriate to consider lifting and transportation loads separately, as they are unique to this form of prefabricated structure.
Although the loading conditions are assessed individually, their combined influence ultimately determines both the global and local structural responses of mining structures. These actions have a direct impact on member forces, deformations, stability requirements, and force transfer mechanisms, all of which must be addressed by the performance of structural connections. Therefore, a thorough understanding of the specific loading environment is crucial for accurately interpreting structural behaviour. When considered collectively, these loading scenarios guide connection design not only through strength comparisons but also by establishing varying requirements for robustness, tolerance to accidental actions, and reliability during handling, transport, and installation. This comprehensive perspective is essential for determining the suitability of connections across various documented applications.

2.1. Gravity Loads

Gravity loads are outlined in Australian Standards [35] and international design codes [31,36] and are generally applicable to mining structures. Structural steel sections (including grating, handrails and stairs) and pipe weights can be determined from three-dimensional structural models [37]. The weight of mining equipment to be installed in the process structure must also be considered; the product vendors provide equipment loads, and the weights are also on the shipping dockets when the equipment arrives. Permanent gravity loads, such as the self-weight of structures and equipment, can be assessed with high accuracy, even though it is common to weigh volumetric prefabrication as part of a quality system and compare the measured result with the theoretical value. The centre of gravity of the prefabricated component is equally important; it is also theoretically determined and frequently confirmed by physical measurement for quality control. For volumetric prefabrication, the centre of gravity and its three-dimensional position are required for lifting and rigging studies, road vehicle transport assessment, sea transport requirements, and support, fastening and lashing requirements.
Gravity loads are important from a strength perspective, particularly in mining structures that are subject to extremely high gravity loads from the stored contents of bins, hoppers, and fluid-retaining equipment. The gravity loads in bins and hoppers are codified with the upper-bound and lower-bound densities required, depending upon the load configuration [38]. However, the Australian Standard [38] for loads in bins and hoppers is conservative [39] and has been withdrawn as the responsible technical committee was no longer active, and EN 1991-4:2006 [36] may be considered as an alternative. Gravity loads also impact the structure’s fundamental natural frequency, influencing the seismic load attracted and determining its distribution throughout the structure. Mining structures differ from conventional structures in that stored material and other gravity loads are usually present. Partial load factors in the Australian Standards consider the statistical variability of the load [40]; however, the Australian loading codes are not bespoke to mining structures, and there may be inconsistencies for unique loading conditions. It is common for partial load factors and their use to be specified in project-specific design criteria [34] as no Australian standard is directly applicable.
Gravity loads also significantly contribute to the second-order (P-delta) effects when combined with horizontal loads and environmental hazards, and these second-order effects must be considered [41]. Other gravity loads include platform- and walkway-imposed actions, stacked material loads, stacked wear/liner plates, equipment change-out and ore spillage, and dust loads. Ore spillage loads can be extreme, and the spilled ore must be removed without further overloading the structure. Figure 2a illustrates extreme spillage loads. A less extreme ore spillage load is shown in Figure 2b. It is usual within the mining industry for these spillage loads to be specified within project-specific design criteria, as these loads frequently exceed the minimum requirements for live loads specified in the relevant design code. It is not unusual to apply a partial load factor of 1 to ore spillage loads; however, this requirement varies according to project-specific design criteria.

2.2. Environmental Loads

Environmental loads include wind and seismic loads, as well as variable loads induced by thermal effects and ground settlements. The occurrence and magnitude of wind and seismic loads frequently depend on the construction site location. Cyclones and tornadoes are associated with specific geographical locations and the seismicity of an area; as such, their occurrence is beyond human control. A ‘climate change’ multiplier of 1.05 has been proposed [43] and is in force within the Australian Standard AS 1170.2 2021 Structural Design Actions Part 2 Wind Actions [44]. Within Australia, the loading codes define geographical locations and the appropriate hazard as a function of the structure’s importance and design life [41,44]. Therefore, the hazard is addressed using probabilistically based criteria [45]. International standards such as the Eurocode EN 1991-1-4: 2005—Actions on Structures—Part 1–4: General Actions—Wind Actions also define wind loading in a similar manner [46]. The mining industry generally applies wind loads from these design codes to structures in a quasi-static manner, with the notable exception being tall, slender structures and those with a low natural frequency, under circa 1 Hz [44]. The loads are assessed either using global drag coefficients or applied to each individual structural member and piece of equipment within the structure. Australian Standards, such as AS 1170.4 2007 Structural Design Actions. Part 4 Earthquake actions in Australia also provide hazard classifications for seismic zones, outlining geographical location, a factor for the site subsoil class and the structure importance level [41].
Whilst temperature is also a function of the construction site location, thermal loads are a manifestation of the structural system employed. The appropriate structural system and releases using sliding joints can minimise the load effect and are frequently employed. This is particularly important in long structures such as pipe racks and conveyors, which may be hundreds of metres long and therefore susceptible to significant thermal expansion. Nonetheless, the thermal-induced actions require identification and consideration during the design process. Thermal effects can also result from the type of refining or process used, or from uncontrolled fire. The effects require consideration from a serviceability, durability, and strength perspective. Appropriate treatment of fire loads has been codified [47,48] and is the subject of further research. Steel structures, which incorporate prefabricated volumetric modules, undergo a reduction in strength and elastic modulus [48,49] and, therefore, lose strength as the temperature increases. The reduction factor used for carbon steel, as used in mild steel beams, is considered during the structural design of high-temperature areas around furnaces and kilns and in pyro-processing plants in the mining industry. These reduction factors are for mild steel and are not suitable for high-strength structural steel [50,51].

2.3. Transient Loads and Operational Loads

Mining structures are subject to transient loads from their surroundings; they are loaded with ore by the mining plant, and the ore is then fed into equipment that sizes, crushes, screens, conveys, and stacks the material. Depending on the process, the structure may be subject to other transient load types, including ore impact, cyclic vibration, fatigue, vehicle impact, and even accidental blast loads.
The mining process generally starts with the ore being fed into the “run of mine” (ROM) bin, and this structure is fed ore by dump trucks or loaders. Loading ore into the bin results in horizontal vehicle impact on the structure and dropped mined material, producing vertical impact loads during unloading. ROM bin layouts, drop heights and vehicle loading are depicted in Figure 3a,b. Horizontal impact loads are frequently taken as 25% of the impacting vehicle’s static mass, and vertical impact loads are assessed using the energy associated with the likely rock fragment’s mass and the fall height. Horizontal wheel loads often impact an inclined surface, raising the vehicle height as it ascends the incline and converting kinetic energy into potential energy, thereby reducing the horizontal design loading.
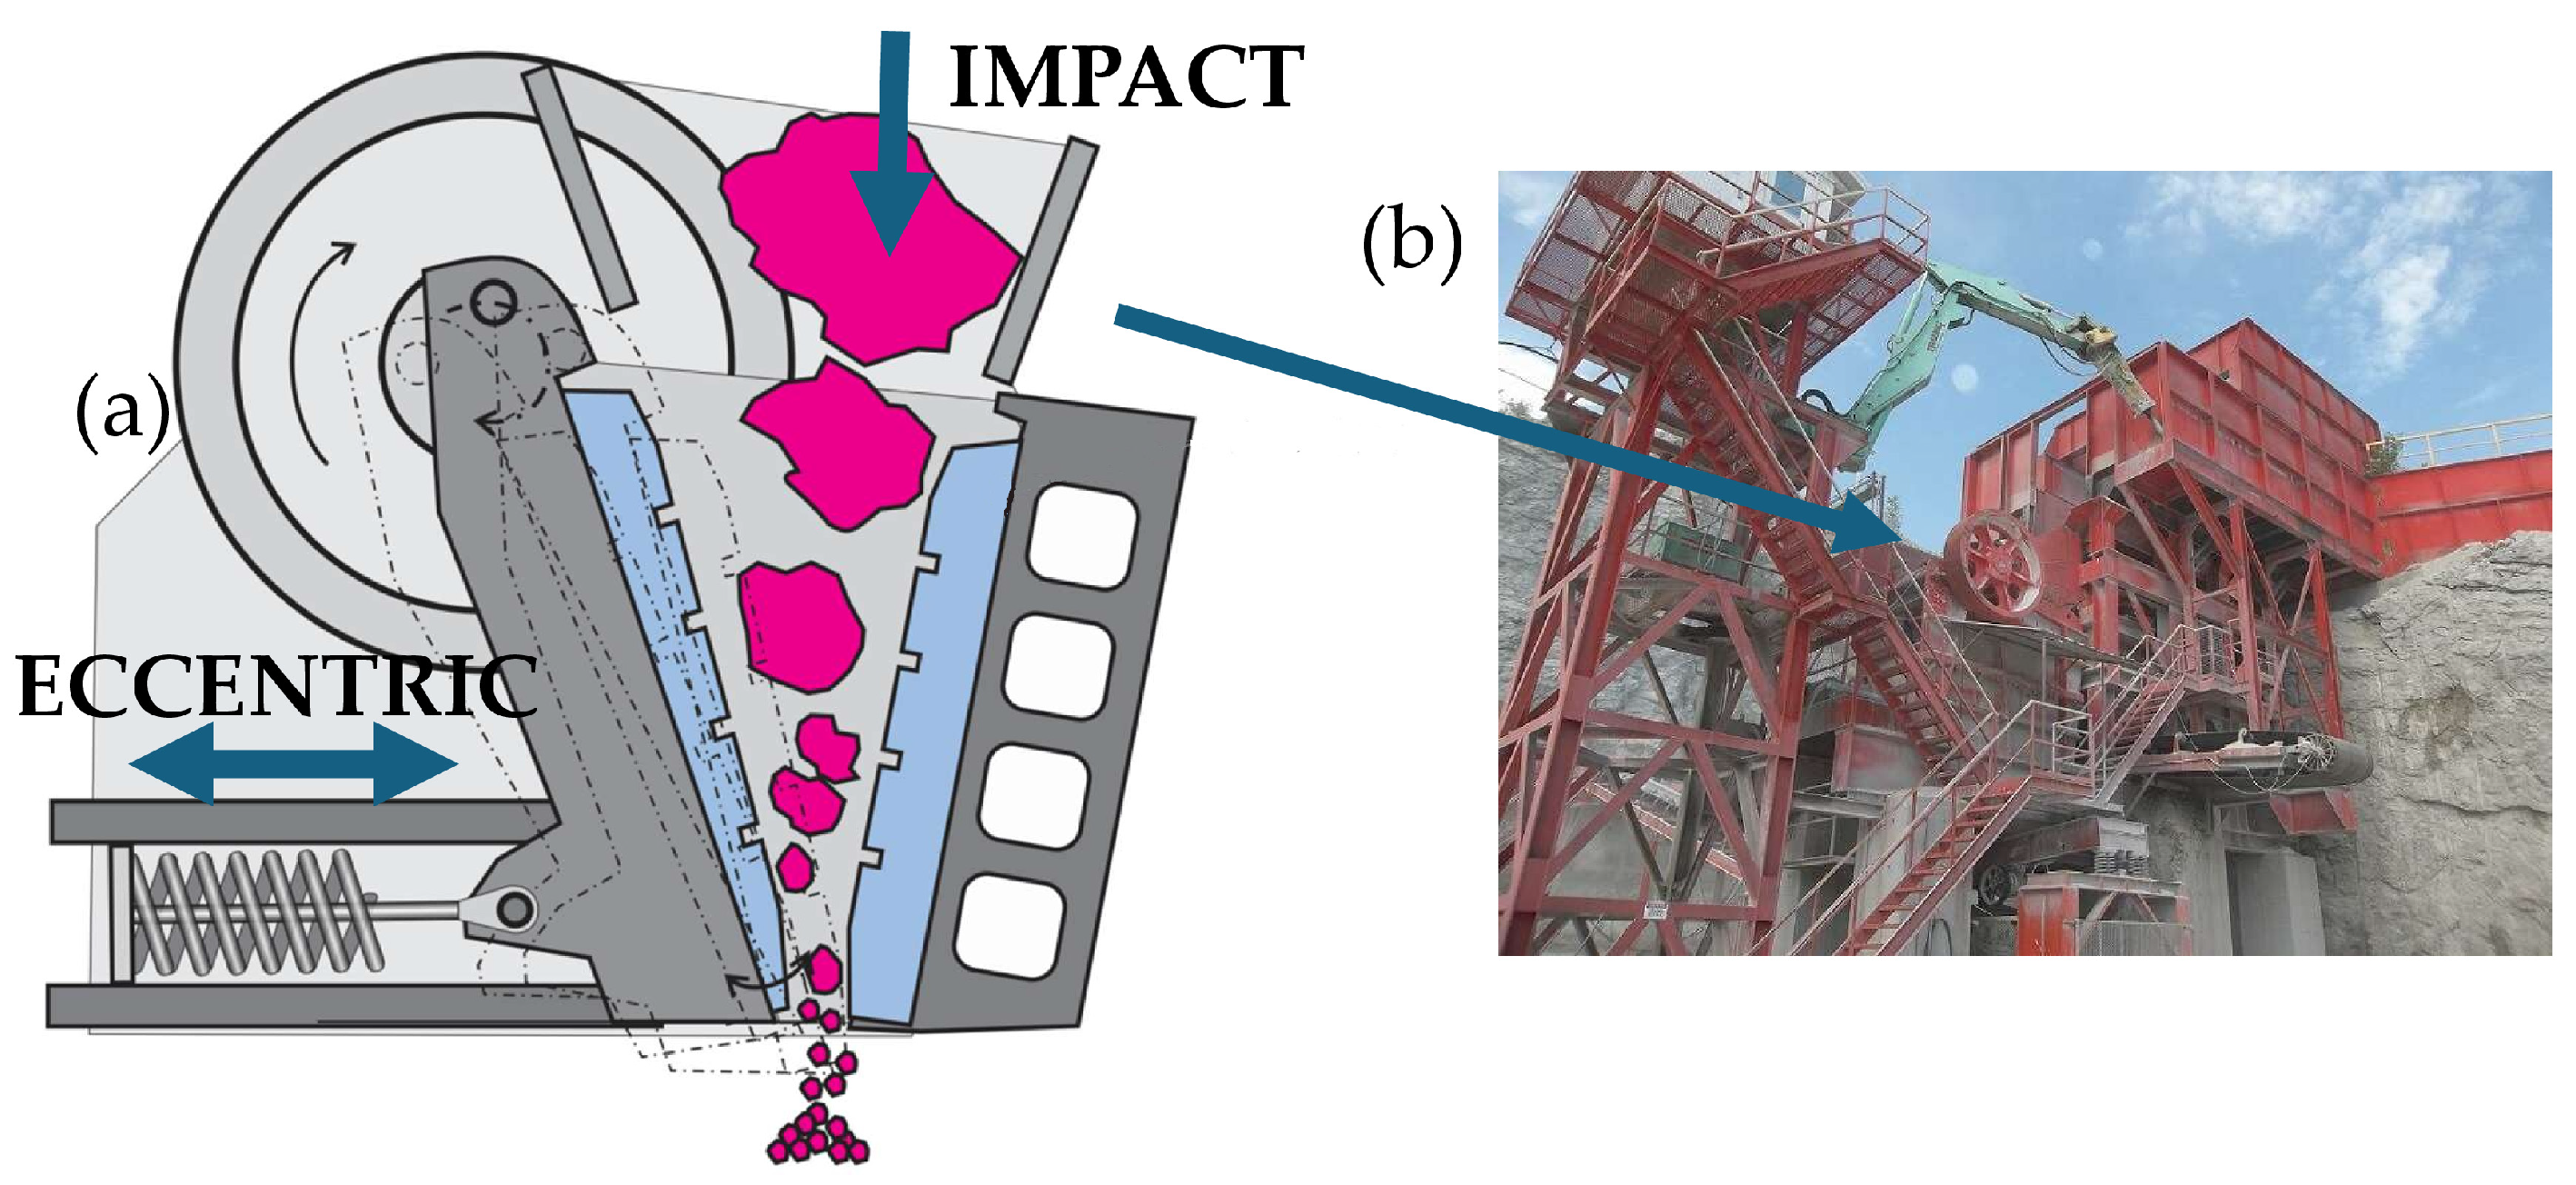
Once the material is tipped into the ROM bin, it is fed into the crusher below at a quasi-constant rate. Jaw crushers frequently have a feeder to regulate the feed flow rate, whilst gyratory crushers may be choke-fed. An example of a jaw crusher is shown in Figure 4a. The jaw moves on an eccentric, with the centre of mass moving sinusoidally, creating a cyclic out-of-balance force. As the ore feed is fed into the crusher, it falls again from the feeder or choke point, resulting in an impact force on the structure. An overall ROM structure, including a run-of-mine bin, a rock breaker and a jaw crusher, is shown in Figure 4b.
The run-of-mine ore may vary in size and shape, and the ROM bin may be protected by an impact-absorbing insertable structural grillage referred to in the industry as a “grizzly”. The grizzly also serves as a sizing device, limiting the rock size that can pass through the bin and into the feeder and crusher. A structure-mounted rock breaker may be employed when the rock size is too large to pass the grizzly aperture. The rock breaker impacts the rock on top of the grizzly, providing high-frequency impact loads both to the grizzly and the rock breaker support structure. An illustration of a rock breaker working above a grizzly is shown in Figure 5a, and the support structure for the rock breaker is shown in Figure 5b.
Conveyors and feeders also result in transient loads transmitted to the structures. Conveyors discharge ore, which frequently has a fall height, at least until the receiving bin is partially filled. Feeders are also subject to this imposed impact load from falling ore. The feeder also subjects the supporting structure to cyclic vibrating loads as the feeding process requires horizontal movement of the feeder. The feeder may subject the structure to cyclic horizontal break-out forces (apron feeder) or high-frequency vibrations (vibration feeder). Feeder arrangements can be seen in Figure 6b.
Mining structures are designed robustly to cope with these transient loads whilst remaining serviceable. Stress concentrations occur around discontinuities, and stress concentration factors can be numerically evaluated by considering the geometry of the discontinuity [60] and various techniques have been developed to mitigate this problem [61]. Connections and weldments for applications in the close vicinity of cyclic and repetitive loading are often detailed with rounded corners or the absence of sharp notches to minimise stress concentrations and reduce fatigue cracking.

2.4. Lifting Loads and Transportation Loads

Prefabrication, by its very nature, necessitates transportation of the product from its place of manufacture to the place of installation. During transportation, prefabricated components are subjected to a range of hazards and load effects, including:
  • Various lifting arrangements with impact factors applied to the dead loads.
  • Self-propelled Modular Transporter (SPMT) loads applied to the prefabricated components as vertical accelerations.
  • Sea transport loads including hydrodynamic and inertial effects, acting across the six degrees of freedom, such as rolling, pitching and heaving.
  • Road transport loads for which inertial effects are designed, considering the three translational degrees of freedom.
Volumetric prefabricated systems exhibit strength and serviceability responses that are highly sensitive to loads induced during lifting, handling, and transportation. This sensitivity arises because volumetric modules are transported and erected as fully three-dimensional structural units, requiring the module to resist significant temporary actions, including global bending, torsion, and local stress concentrations that may not govern the in-service design condition.
In contrast, hybrid modular structures are typically fabricated, transported, and lifted as flat-packed, two-dimensional panelised components. These elements experience comparatively lower lifting and transportation demands due to their reduced self-weight, simpler load paths, and greater flexibility in support conditions during handling. As a result, the structural performance of hybrid modular systems is generally less influenced by construction-stage actions, with strength and stiffness demands being more closely aligned with their final assembled configuration. This characteristic provides an advantage over conventional modular systems.

2.4.1. Lifting Loads

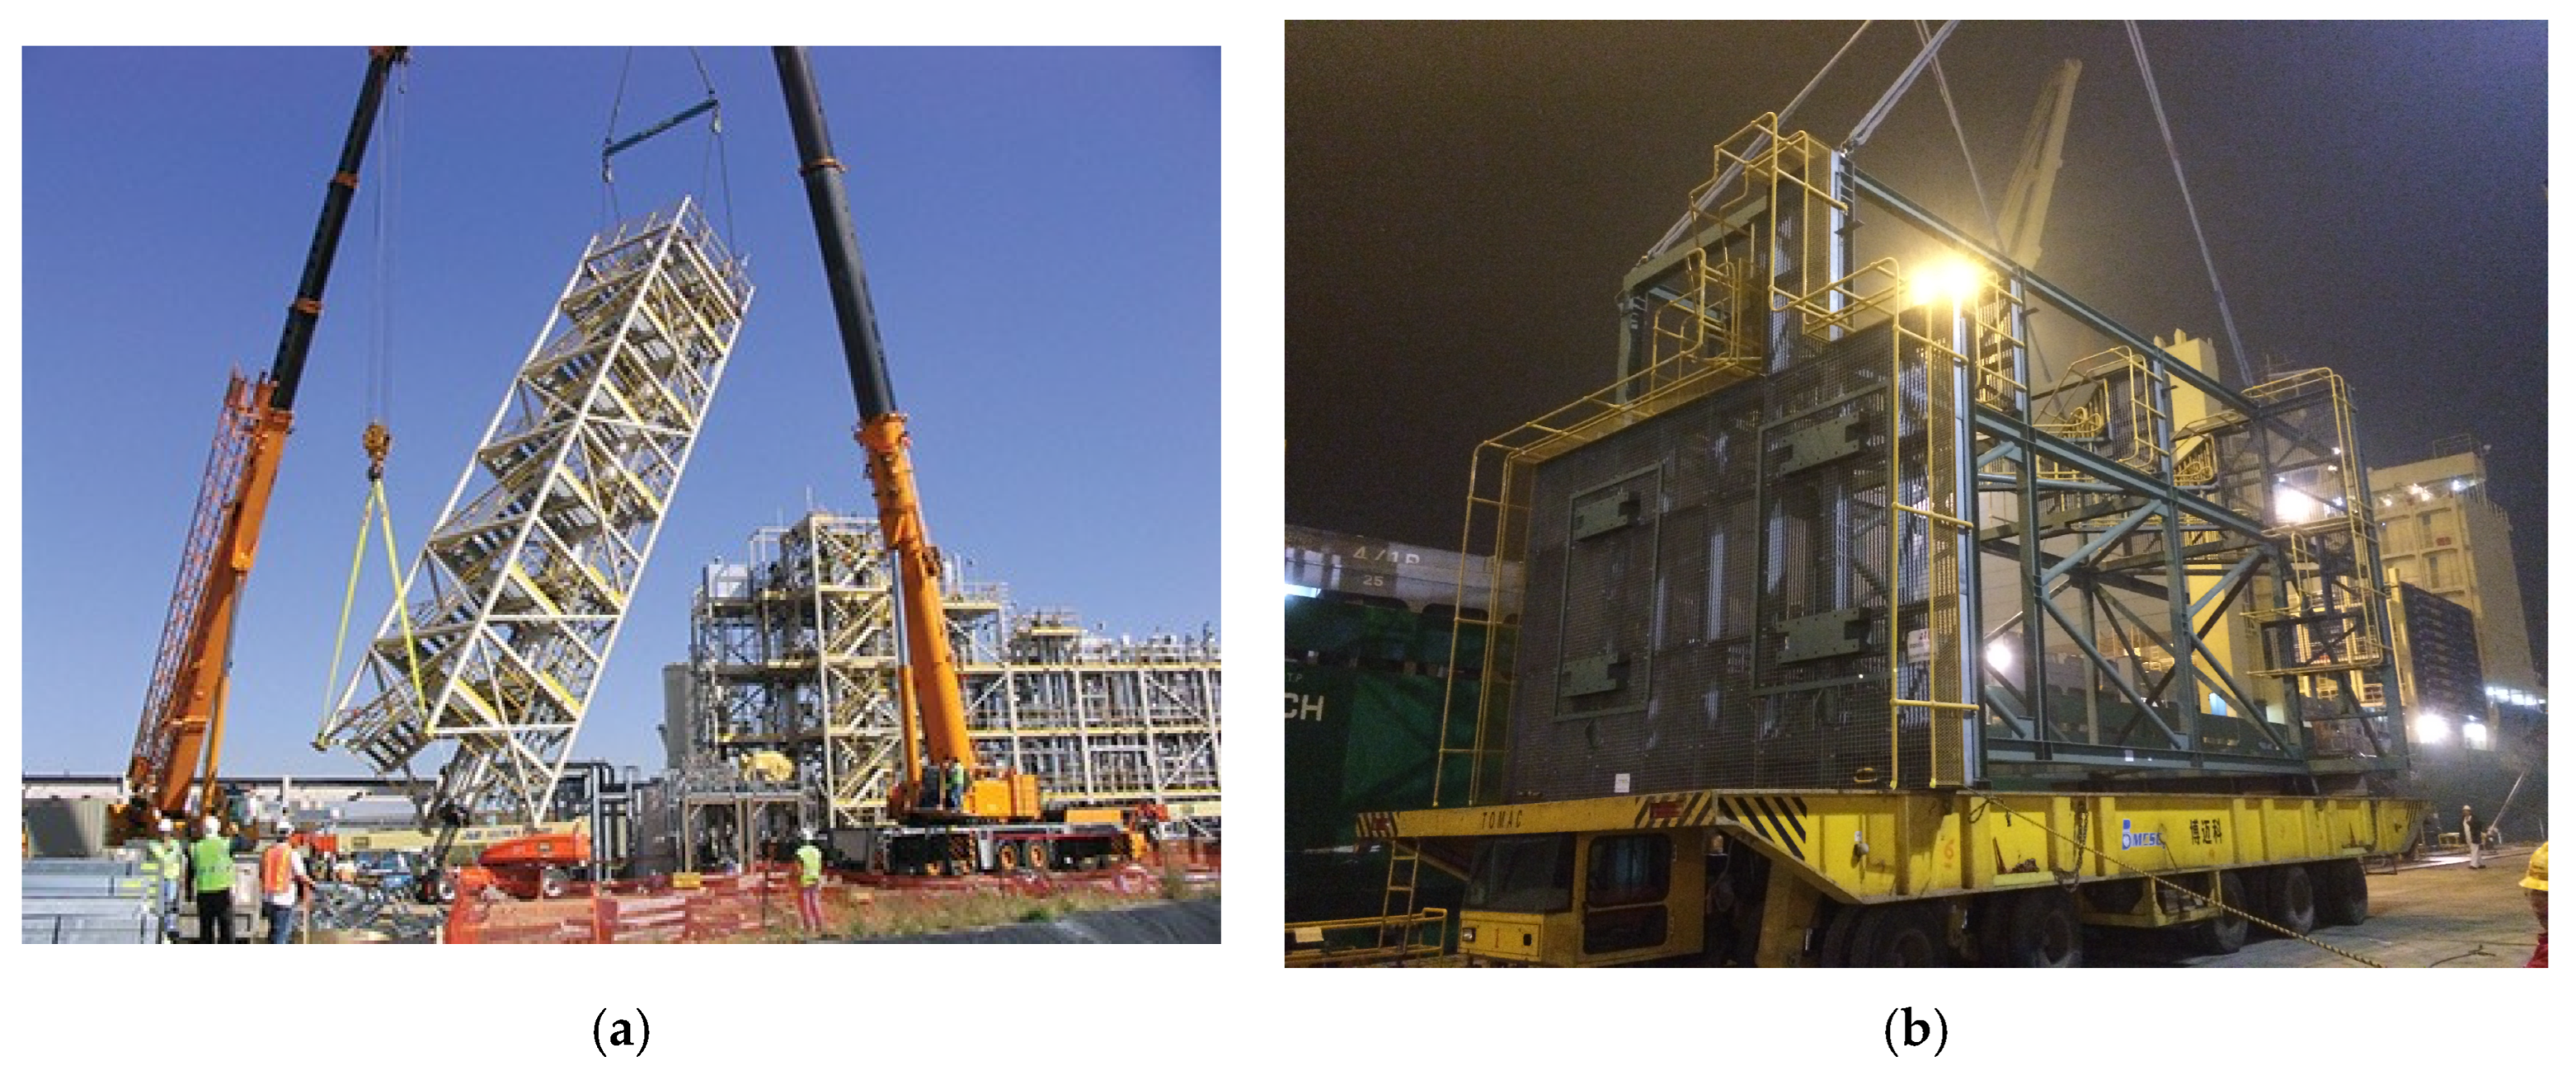
Lifting consists of three distinct variations: direct vertical lifting (generally one crane), a double lift to stand prefabrication from a horizontal to the vertical position (generally two cranes, as shown in Figure 7a) and a horizontal lift for placing the structure flat during transportation (shown in Figure 7b). Depending upon the size and aspect ratio of the volumetric module, it may be constructed in a horizontal orientation and then lifted vertically, or a vertical volumetric module may be laid on its side to facilitate transportation or shipping. In either case, the volumetric module is supported in a manner that may be very dissimilar to its final support configuration [62]. Crane studies must consider each type of lift and location on the site [63]. Impact factors range from 1.35 to 2.0 [64,65,66] times the weight of the structure for general structural design, through to factors of up to 2.7 for local lifting eyes and beams when including load factors [35]. Lifting devices are generally required to be proof-loaded; the proof load level is to be in accordance with Australian Standard AS 4991-2004 [67] Lifting Devices [68] and is a function of the lifting device’s capacity. These factors are generally decided at the project study stage and documented in the project design criteria.

2.4.2. Self-Propelled Modular Transporter Loads

Self-Propelled Modular Transporters (SPMTs) are not operated on perfectly smooth and flat ground; therefore, inertial forces are introduced when moving the volumetric module. Recent studies have shown that vertical accelerations due to SPMT movements can vary between 0.38 and 2.3 gravities, depending upon module weight and SPMT speed [69]. The SPMT spreads the volumetric construction’s weight over the transporter’s numerous wheels [70]. SPMTs are also used in roll-on roll-off (RoRo) situations when loading a prefabricated module directly on a barge by driving the SPMT from the wharf to the barge. The height of the wharf deck and the barge are matched by tide and buoyancy. However, some dimensional height discrepancies persist due to imperfect alignment. In any event, the bridge section has “structural depth” to support the wheel loads of the SPMT. The landing stage must have enough strength and stiffness to ensure the SPMT can traverse across to the barge safely [71]. The net result is that the SPMT-induced transportation loads must be considered for all aspects of its use in module movements.

2.4.3. Sea Transport Loads

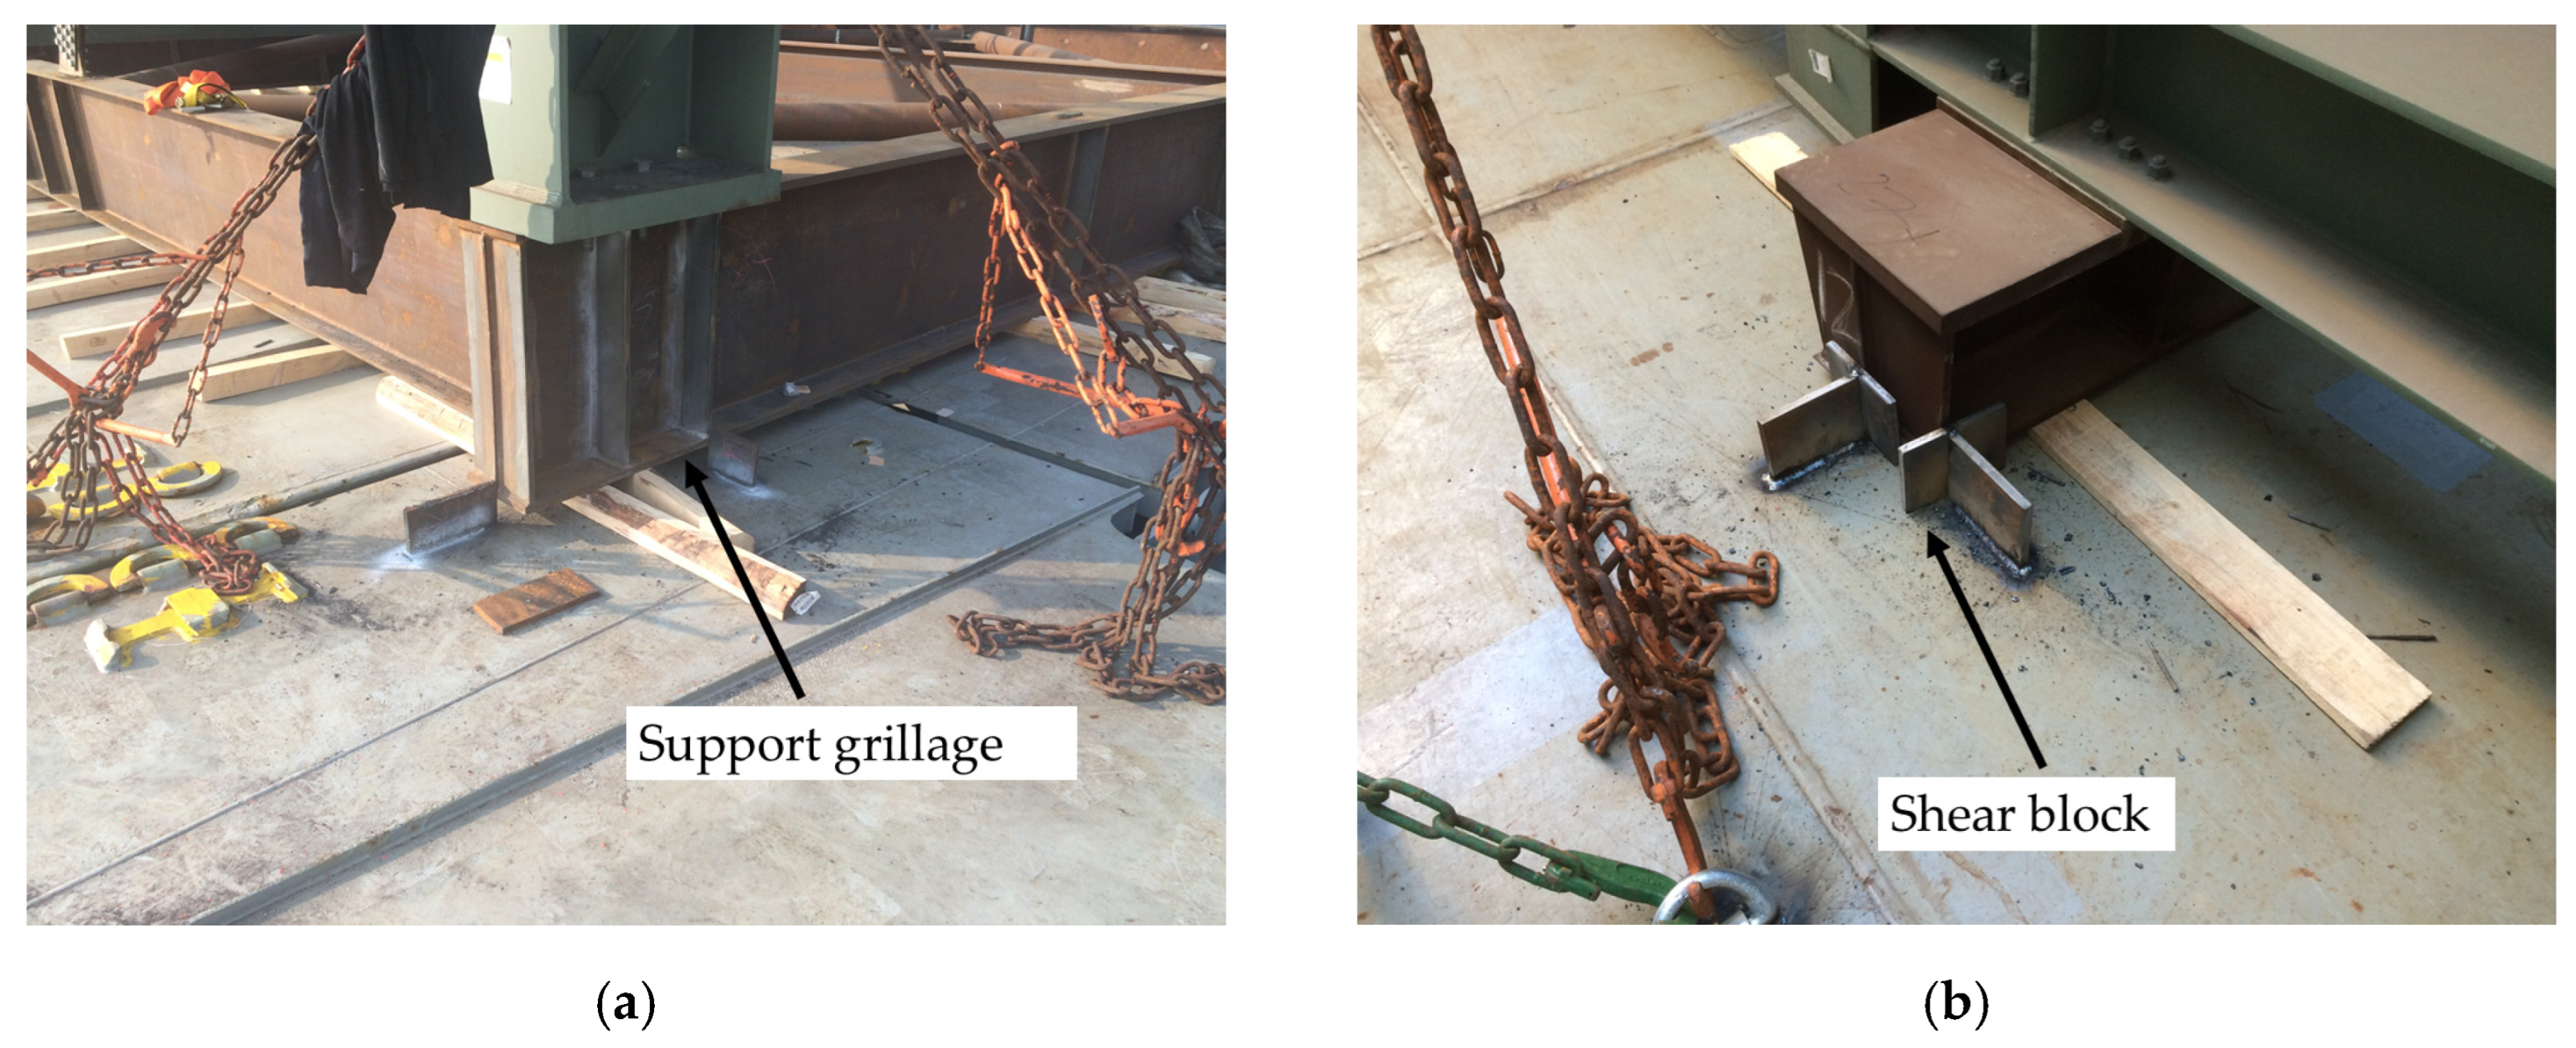
Volumetric construction must have sufficient strength and robustness to withstand ocean-induced inertial forces. Sea transport loads depend on the vessel’s size and draft, the cargo’s location (deep in the hull or on deck) and its position relative to the centre of buoyancy, and the voyage route. The Code of Practice for Packing of Cargo Transport Units [72] provides generic guidelines as to longitudinal traverse and vertical accelerations, as shown in Table 1. Route-specific cargo calculators are also used for this purpose [73]. There is also the hydrodynamic interaction between the volumetric module, the ship, and the ocean to be considered, as well as sea slamming [74]. When a prefabricated module is transported by ship or barge, it is subject to the structural self-weight, any operational wind and the acceleration in the six degrees of freedom that the vessel may move; that is, rolling in each direction, pitching in each direction and heaving up and down [75]. Sea fastenings must resist these accelerations and resulting loads, as must the support grillage, the prefabricated construction and the vessel attachments. Naval Architects are frequently engaged to assess these impacts and to formulate a design criterion in light of the chosen transportation route [74]. Sea-fastening attachments include welding temporary shear blocks to the ship’s structure at main support points to prevent sliding and installing inclined lashings to assist in overturning stability. The support grillage, shear blocks and inclined lashings for a smaller volumetric module can be seen in Figure 8.

2.4.4. Road Transport Loads

Road transport loads have attracted increasing interest, as they play a critical role across numerous industries beyond mining. However, there remains limited consistency in the definition and application of transport design loads. Soules highlights this variability [76], and identifies a lack of uniformity across industry practice in selecting representative acceleration demands for road transport.
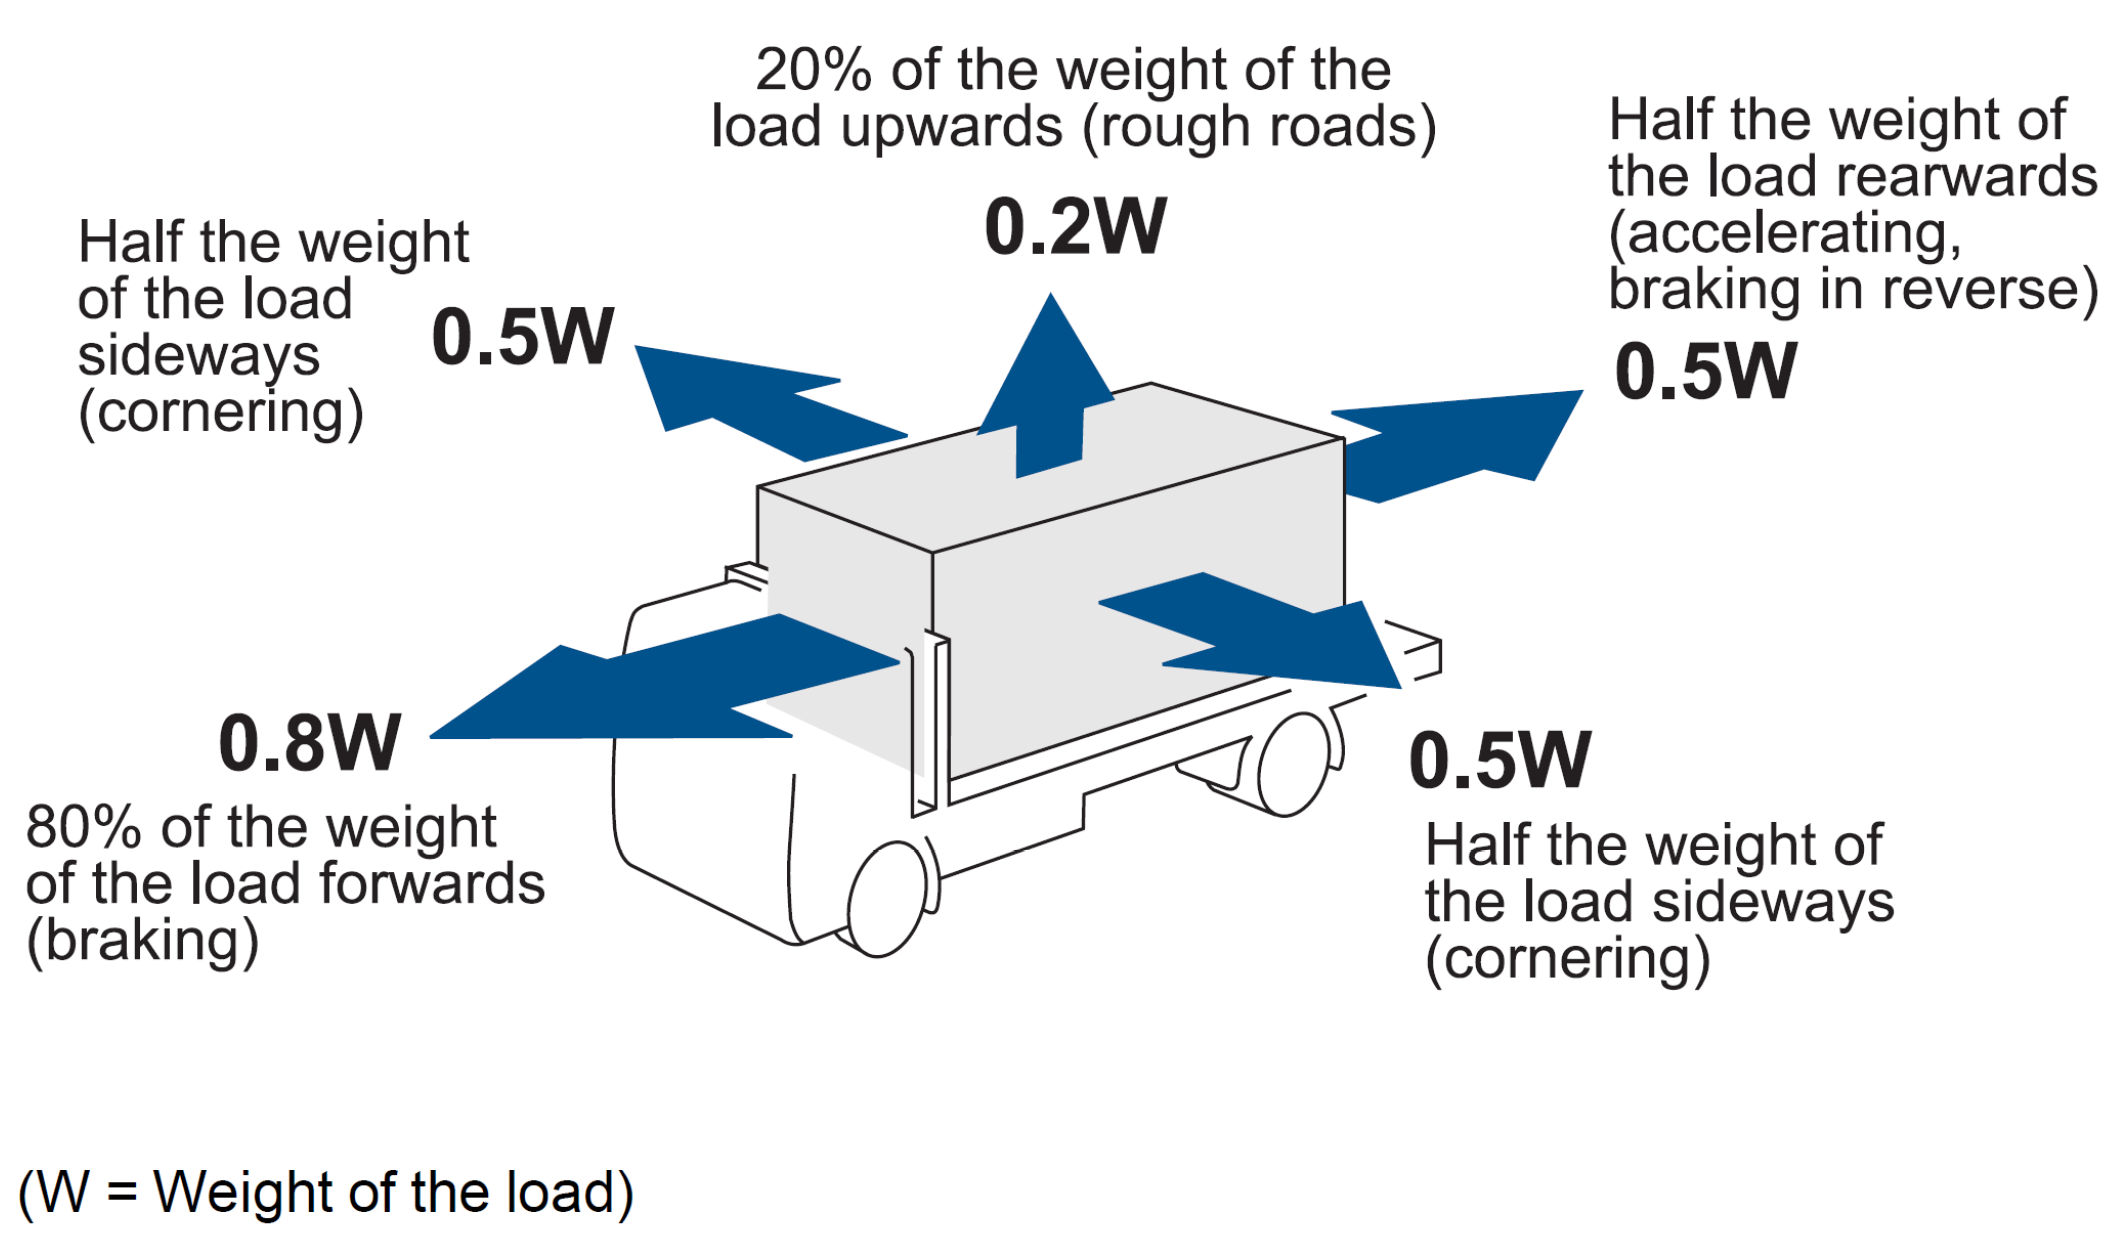
In Australia, the National Transport Commission (NTC) has developed guidelines for transport loads intended to provide a consistent reference basis for design [77] and is illustrated in Figure 9. A comparison between these guideline values and reported industry practice illustrates the NTC’s broad positioning and relative conservatism in accommodating the inherent uncertainty in transport conditions. Transport loads can materially influence structural design outcomes, both in global member actions and in the design of load-restraint and tie-down systems. Consequently, road transport design assumptions are typically established during the project study phase and formally documented within the project design criteria for mining and modular infrastructure projects.
Reported industry data indicate that truck transport can impose a wide range of acceleration demands on structural components and their connection systems before installation. Based on investigations compiled by Soules et al. [76], longitudinal (in-line) accelerations during truck transport have been reported to range approximately from 5% to 80% of gravity, reflecting variations associated with braking, acceleration, and road surface conditions. Transverse accelerations acting across the vehicle are generally lower but remain non-negligible, with reported values ranging from approximately 3.5% to 50% of gravity, depending on vehicle dynamics, load restraint effectiveness, and cornering behaviour.
Vertical accelerations, acting perpendicular to the transport deck, exhibit the greatest variability, with reported ranges extending from near zero up to 100% of gravity, particularly under rough road conditions. Although transport-induced loads are typically short-duration and highly variable, they remain relevant to connection detailing and robustness considerations, particularly during handling, transport, and installation. Accordingly, these reported load ranges provide contextual information for assessing connection suitability rather than serving as a basis for direct structural performance comparison.
The loading conditions discussed above—encompassing transport-induced accelerations, impact-type actions during handling and placement, and cyclic or repeated loading scenarios—are characterised by significant variability in magnitude, duration, and point of application. While many of these actions are transient and may not govern ultimate limit-state design, they can impose critical demands during handling and installation and may influence detailing requirements at connection interfaces. As such, their significance lies not solely in peak load magnitude, but in their implications for robustness, tolerance to accidental actions, and reliability under non-standard loading scenarios.

3. Structural Response of Mining Structures

As described in Section 2, prefabricated mining structures are subjected to gravity, environmental, transient, operational, lifting and transportation loads. The structural response of each type of these loads is addressed in Section 3.1, Section 3.2, Section 3.3, Section 3.4 and Section 3.5. and the discussion is cognisant of the industry’s successful and frequent use of standardised bolted connections and the design office modelling techniques employed. It is imperative that the global structural response is not adversely affected by the choice of connection and can be adequately modelled in the design office.
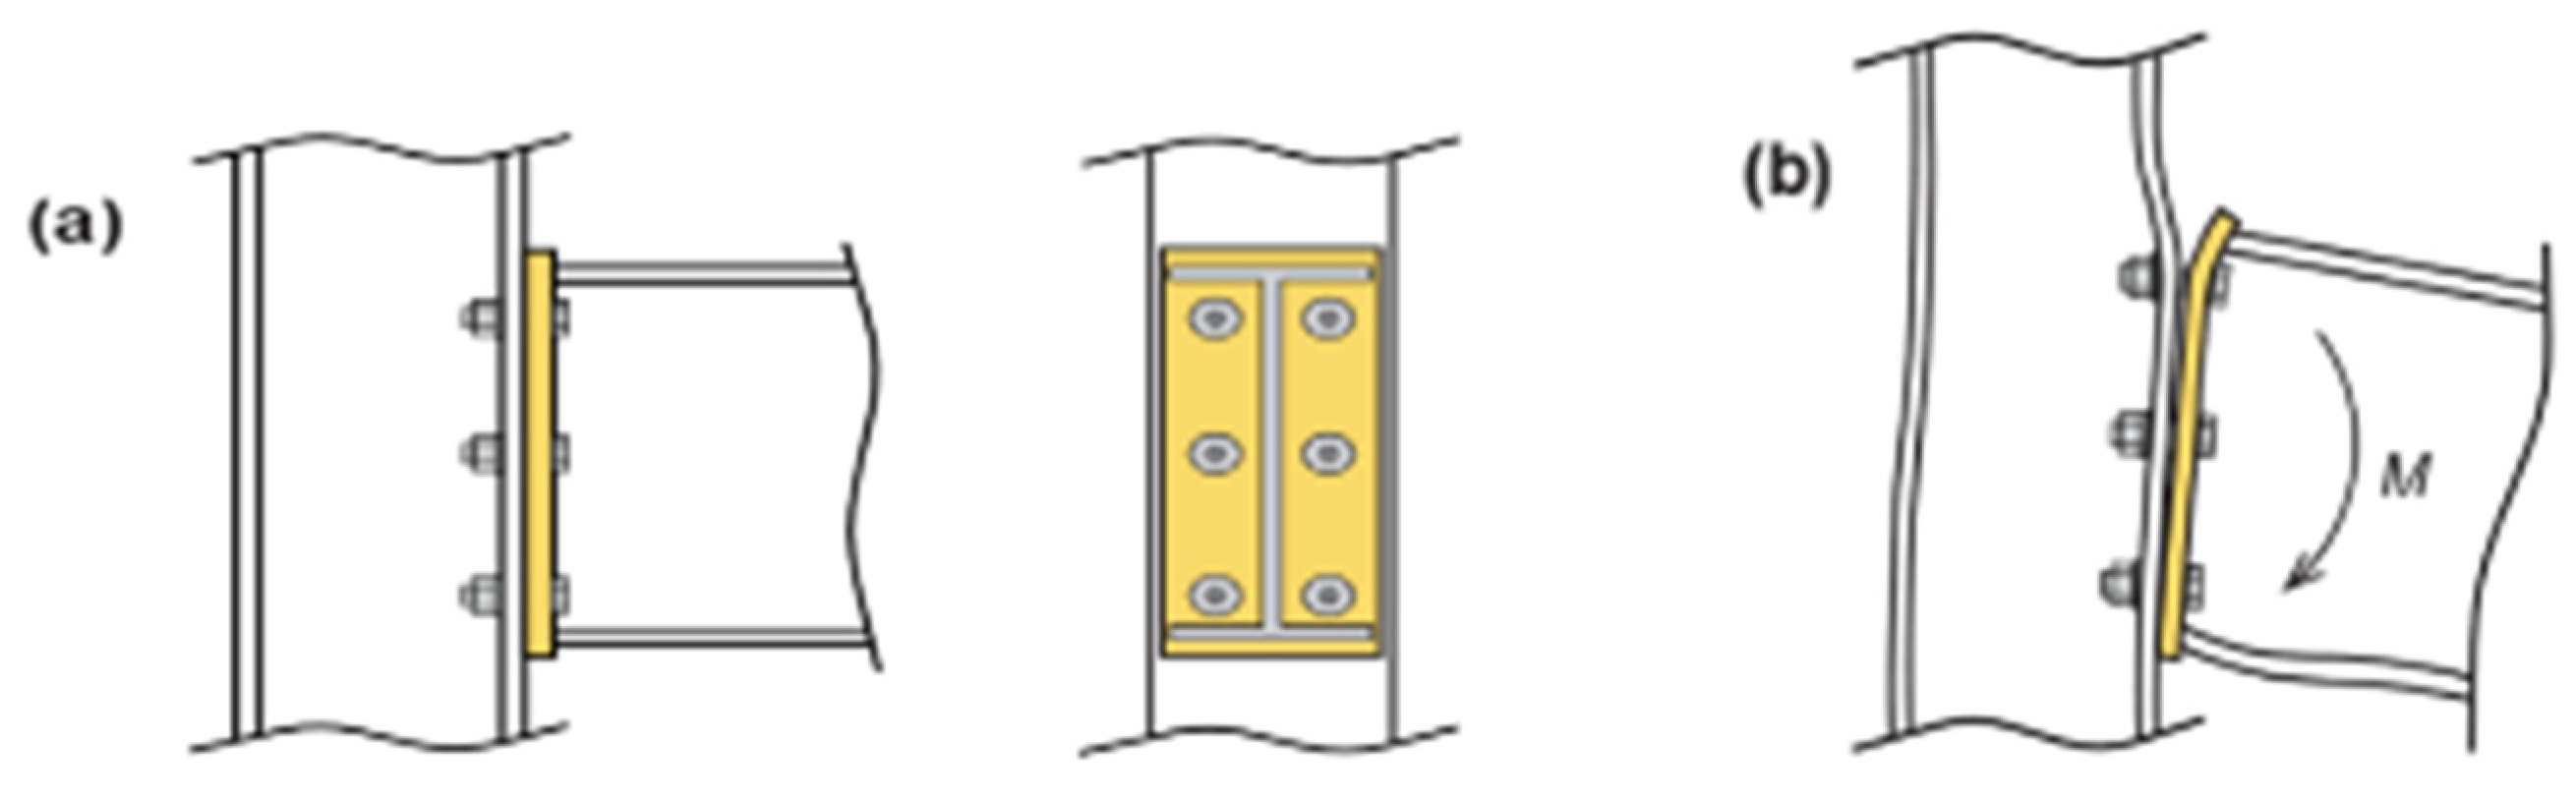
While there have been 136 recorded mining structural failures in Queensland and Western Australia since 2001 [78,79], they have yet to be attributed to connection design inadequacies. An extrapolation of the cause of the failures is that the currently used connections perform adequately and safely, and that any new connection must perform equivalently or be superior to what is currently used. In the mining industry, connections between beams and columns are commonly made with bolted flange endplates (FEPs), with field welding of structural connections the exception and generally avoided. The FEP beam–column connection has been extensively researched [80,81] and tested, and is well understood regarding rigidity, slippage, and moment–rotation relationships. A FEP and its deformation behaviour are illustrated in Figure 10. The performance of FEP beam–column connections is widely accepted as satisfactory throughout the mining industry. It can be used as a comparative benchmark to assess the structural performance of newly developed connections. Any alternative connection performance should at least be comparable to the benchmark FEP performance regarding the joint response (including force displacement, moment–rotation, and slippage behaviour) and the global structural behaviour (including serviceability and second-order effects), as well as the ability to undergo load reversal and behave in a ductile manner.

3.1. Response to Gravity Loads

Mining structures are typically constructed from hot-rolled steel sections that form braced and sometimes portal steel frames. The behaviour of such structures is well understood and easily modelled in the design office using commercial frame analysis software. The member connection response used in most commercial software in the design office does not consider non-linear semi-rigid behaviour, with either fully fixed or pinned behaviour preferred. It is possible to model “linear spring connections” using dummy members and the like, though this is not normal design office practice. FEP connections typically behave as semi-rigid connections [83] that are non-linear. Semi-rigid and non-linear behaviour is frequently ignored in engineering design offices, and this approach is readily accepted and conservative. FEP connections are assumed to behave as pins, and the truss action of end-frame vertical bracing provides the structure’s lateral stability. Such an assumption is justifiable due to the ability of these connections to rotate at the joint without distress due to the ductility of these types of connections. Furthermore, design offices are unlikely to have agreed and audited moment–curvature models for routine design, favouring simple, transparent and robust structural systems that avoid added risk. Therefore, a “structural pin” is a conservative, risk-free lower bound for most routine designs. The ideal connection detail should either have the ductility to behave as a pin or possess sufficient stiffness to act as a fixed-end connection, as engineering design offices are rarely equipped to analyse and model the structural response of semi-rigid non-linear connections that cannot be modelled as pins. The alternate connection detail should also support a construction methodology that results in a safe and stable structure under gravity loads (and the notional horizontal load) [84] before installing bracing to carry in-service lateral loads. Construction verticality and dimensional tolerances must also be complied with [85] to ensure the structure does not have built-in racking issues. Understanding the initial moment–rotation and slip response behaviour of newly developed alternate connection details is fundamental to the structure’s initial response and to modelling its response for design loads.

3.2. Response to Environmental Loads

As discussed in Section 2.2, environmental loads include wind and seismic loads and loads introduced by thermal effects and ground settlements. Both wind and seismic loading effects depend on the structural response and the structure’s fundamental modal frequency [41,44]. These horizontal loads are generally transmitted to the foundations by a bracing system or, in some instances, by portal action. The primary goal of a mining structure is to support mechanical equipment and metallurgical processes, allowing a mined product to be beneficiated efficiently; the structures are largely auxiliary items laid out and placed for that sole purpose. Mechanical and process suitability, therefore, takes precedence over structural form. Equipment weights vary between levels. Mechanical chutes, pipework, and conveyors are placed above and below the equipment and frequently offset horizontally for process reasons. The result is that mining structures rarely possess uniform or symmetrical mass distributions or uniform and symmetrical stiffness. Offset mass from the centre of stiffness also results in high ductility demands and non-uniformity of seismic load distribution [86]. The approximations presented in the Australian Standards [41] for the structure’s modal frequency based on building height and bracing type are of limited applicability due to the non-uniformity of the structural form [87]. Whilst some of these structures may comply with the definition of Earthquake design category II for quasi-static analysis as described in the Australian Standard [41], such structural forms are unsuited to quasi-static analysis for seismic loading, and dynamic analysis is better suited to accurately predict the structural response [88].
The FEP connections currently used for bracing and portal action exhibit ductile, safe, predictable behaviour under environmental loads, and any alternate connections must do the same. The structural stiffness of any alternate connections is used to assess load distribution and the fundamental modal frequencies in dynamic analysis. Fundamental modal frequencies are numerically evaluated at zero strain; hence, understanding the small-strain structural stiffness of the beam–column and bracing connections is required to understand the structural response to the predominant environmental hazards. Whilst rarely used in the design office, a forced response analysis eliminates the need to determine modal frequencies and, hence, the small-strain dilemma.
By their very nature, differential settlements result in dissimilar ground movements across a structure, which causes global tilting and leaning. The movement causes relative displacements throughout the structure, reflecting on the beam–column actions and magnifying second-order effects. The structural response due to the differential movement of column bases in a braced mining-type structure invariably results in design actions exceeding section capacity and overstressing the section. When a mining structure subject to uneven settlement contains sufficient robustness or rigidity, the foundation can “hang” on the column base plate, no longer providing vertical support and altering the structural system and expected behaviour. Differential settlements, when they occur, are generally unexpected and best dealt with by manual re-levelling of the structure using shims at the base plate level. Mining structures are seldom designed to resist differential settlement directly; movement adjustment strategies are the preferred approach.

3.3. Response to Transient and Operational Loads

Mining structures are subjected to transient loads; they are loaded with ore by the mining plant, and the ore is then fed into equipment that crushes, screens, conveys and stacks the material. Depending upon the process, the structure may be subjected to other transient load types, including impact loads, maintenance loads, loads due to changes in the direction of material flow, cyclic vibrating loads, fatigue loads, wind loads, earthquake loads, vehicle impact loads and even accidental blast loads. Structural detailing near cyclic loading frequently includes rounded corners and the lack of sharp notches to reduce fatigue cracking. Cyclic stresses are kept below the fatigue endurance limit, structures contain direct load paths, and connections provide ductile responses. The structure must respond to these transient loads appropriately, ensuring that fatigue endurance limits are not exceeded [84] and that the structure’s serviceability criteria are maintained when subject to these ephemeral or continuing loads. Human comfort levels for vibration exposure vary between the different areas of the plant and the length of human exposure, and the acceptance criteria are provided in the Australian Standards [89,90]. For example, the acceptance criteria for a working platform differ from those of a control room when considering compliance with human comfort levels for vibration exposure. Transient loads can also adversely affect motors and other electrical equipment, and resulting component velocities must be considered in the design.
A full assessment and description of these transient loads is beyond the scope of this study. See Table 2 for typical equipment and the transient loads used within the industry associated with a mining process plant. Importantly, Table 2 highlights that mining structure connection details frequently require consideration of not only the typical static and environmental loads but also cyclic, dynamic, and impulsive loads and fatigue considerations. In this regard, mining structure connections require greater scrutiny and greater robustness than conventional structural connections.

3.4. Response to Lifting Loads

The prefabricated structures’ response to lifting loads differs from the response required during operational service. During the lifting stages, components are temporarily subjected to design actions that differ from their operational design conditions in terms of location, direction, and magnitude. Lifting points are usually best located at nodal or triangulated points, with the aim of limiting bending loads induced by the lift and maximising truss-like axial response, thereby maximising component stiffness by utilising truss action rather than flexure. Lifting frames are frequently used to eliminate horizontal force components resulting from inclined stings, limiting the design actions to the structure’s self-weight and impact factors and facilitating the required lifting studies. Landing points, the support location at the end of the lift, are also preferentially designed at stiff triangulated points to eliminate bending and possible damage from web crippling. Lifting response may also dictate the need for temporary bracing, often referred to as transport steel, to ensure intended load paths and structural robustness.

3.5. Response to Transport Loads

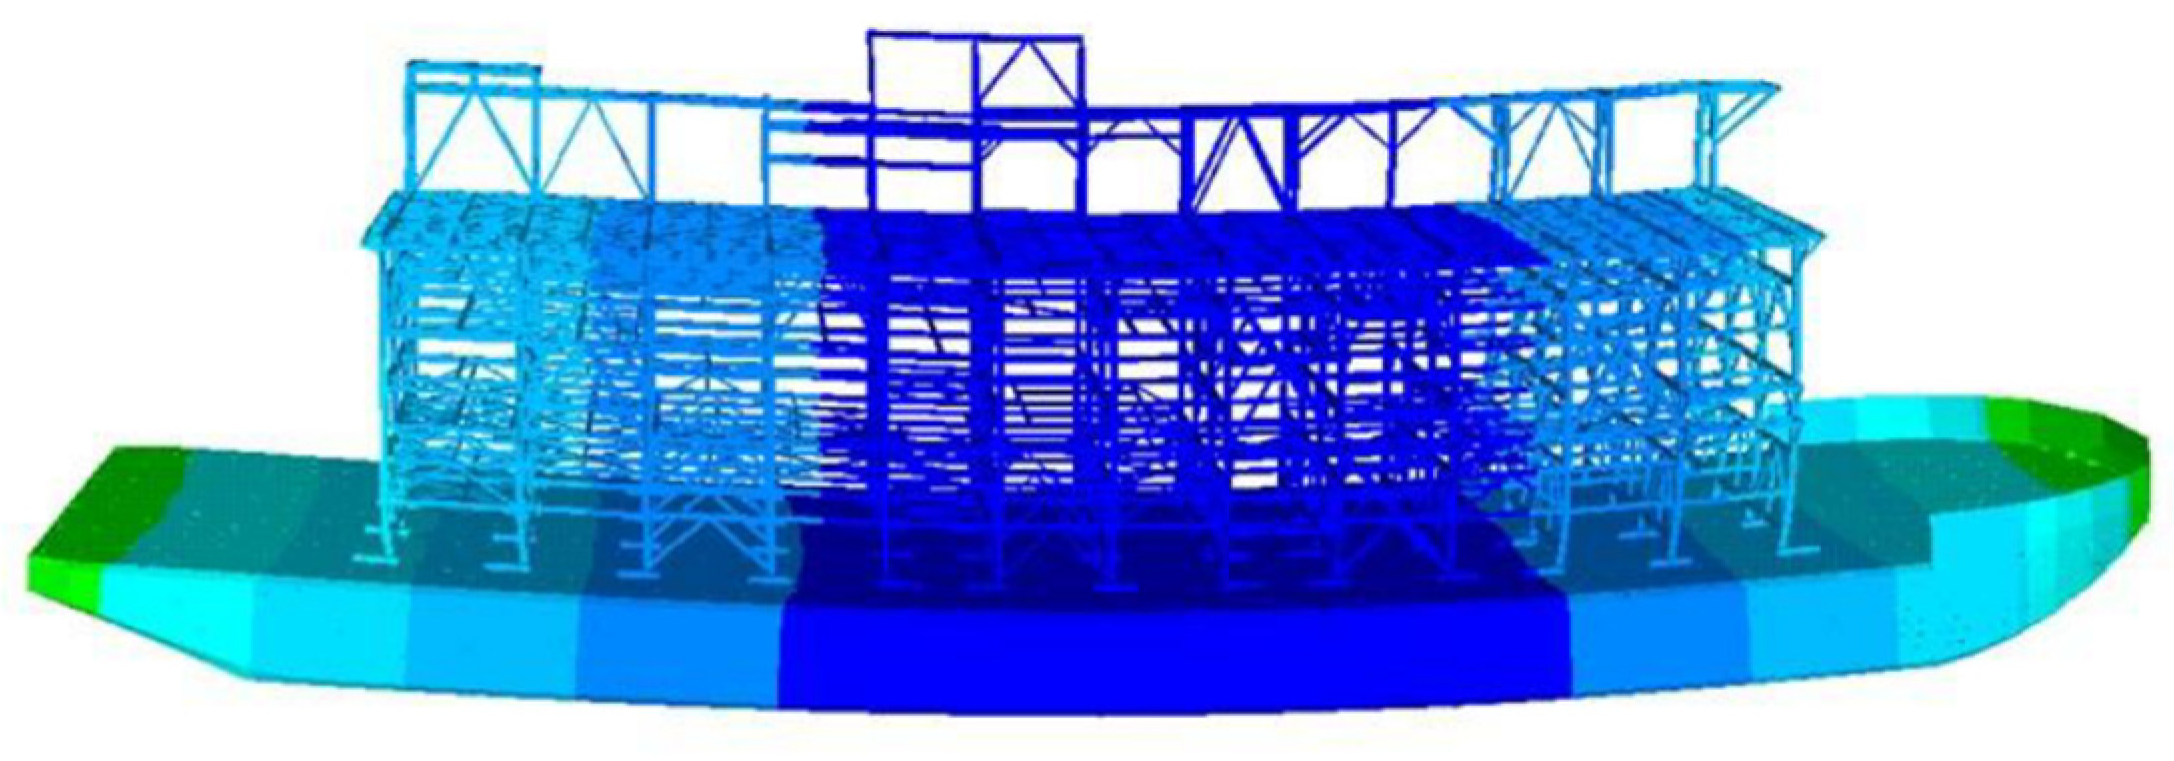
Each transport type load may be different in magnitude and direction. Each transport support configuration is also potentially different. The differing loads and points of support elicit different internal force distributions and, hence, different structural responses. For example, a volumetric structure is lifted from lugs at the top (support case 1), supported on an SPMT by temporary transfer beams between columns at multiples of the transporter width (support case 2), supported on temporary stools or base plates with horizontal included lashings up to some height in the structure (support case 3) and supported at the width/length of a road trailer (support case 4). It is common for these four support cases to all be different from the final installed support location. Each support case must be analysed, and the structure’s suitability assessed in terms of strength, serviceability, lashing details and local concentrated loads. Sea transport loads are typically considered as pseudo-static loads for module strength and stability; however, on larger and complex modules, the vessel interaction with the hydrodynamic behaviour may be analysed as an integrated hull and module structural model [74] as demonstrated in Figure 11.

4. Key Requirements for Connections in Hybrid Mining Structures

Key requirements for hybrid mining structures highlight the need for construction approaches guided by suitability and draw attention to major challenges and limitations associated with both current and emerging connection systems used in mining operations.

4.1. Zero Harm During Erection

Workplace safety and zero harm are principal requirements within the construction industry [1] and are, in fact, codified within Australian law [91]. New concepts must consider worker safety and avoid placing a worker on or under a suspended load, and if at all possible, remove the worker from the danger zone [92,93]. Connecting hybrid components inevitably involves working at heights. Working at heights requires elevated work platforms, and to do so safely requires safety rails, body harnesses and anchor or tie-off points [94,95]. Thus, the ideal connection should be designed to avoid placing personnel on a suspended load, removing the hazard of working on an elevated working platform, and the risk to the person.

4.2. Alignment Without Human Intervention

When assembling prefabricated panels onto vertical frame components, the frame component will generally be in position, whilst the horizontal panel part of the assembly is lifted up under the guidance of the dogman, suspended on the crane’s hook. The frame and panel must join at exact points to form the final hybrid structure, with the final tolerance less than a few millimetres. When the suspended component is in close proximity to the fixed component and about to join, the optimum connection will assist the process without further human intervention [1]. This can be done by an aligning mechanism that, when lowered, uses gravity to adjust the final position. The aligning mechanism must have adequate tolerance to slide into place, allowing the suspended component to slide freely into its intended location. The aligning mechanisms may be angled plates or circular tapered guides; the main prerequisite is to facilitate joining prefabricated panels without initial human intervention at the point of contact.

4.3. Constructability and Tolerances

Fabrication and erection tolerances of steel structures are specified in the design standards. In the case of the Australian Standard AS 4100:2020 Steel Structures [84], there is a complete section devoted to fabrication and a second section to erection. Various methodologies for determining the position and verticality of structural steel components have been explored [85], including those used in mining-type structures such as train load-out facilities. Whilst the body of knowledge is tried and tested, it is mostly based on conventional construction techniques, stick-built erection, resulting in global final positions. Whilst final structural building tolerances apply to mining structures, appropriate erection clearances are a prerequisite for assembling large prefabricated components, and clearance requirements must be cognisant of a large frame’s spatial and volumetric characteristics compared to an individual stick component. During the joining of hybrid structures, the vertical prefabricated frame components will often be fixed in position [1], whilst the horizontal prefabricated panel component is maneuvered into position. The component being maneuvered must sit between the fixed spatial points whilst suspended from a crane hook, and the large, zero-tolerance components become problematic. Therefore, the desired connections between the prefabricated components must be cognisant of the spatial need to manoeuvre the suspended prefabricated component between the fixed-in-position components. Appropriate clearances are required to assemble such components. Fit-up or assembly studies will be required, as the success of any novel connection will depend not only on its structural performance but also on its ability to accommodate the inherent tolerances of these types of structures.

4.4. Erection and Partially Completed Structures

At all times during the erection process, structural stability is fundamental for safety [96] and from a property protection viewpoint, and it is the design engineer’s responsibility to provide appropriate guidance [97,98]. This applies to stick-built [99] and hybrid modular structures assembled as panel-and-frame components. Stability during erection requires consideration at both the design and planning stages. Prefabricated frames must be designed to be structurally stable when initially stood up. The foundations and base plates must be designed to provide sufficient lateral and overturning stability. Any proposed beam–column connection detail must be cognisant that it forms part of a partially erected structure, and any suitable details require some degree of force/moment and shear transfer ability in their unfinalised state [1]. Thus, an ideal connection will assist stability as soon as it is placed in its final position.

4.5. Structural Robustness

As outlined in Section 2, mining structures are unique in that they are not only subjected to hazards typical of conventional structures; they are also subjected to a variety of additional transient loads due to the nature of their intended ore processing purpose during the operation. As detailed in Table 2, mining structure connections may be subjected to sinusoidal varying transient loads, causing global structural dynamic response, which results in local and connection-based fatigue issues. Similarly, mining structure connections are subjected to impact-type loads from various equipment and vehicles for example. A key requirement for connections in hybrid mining structures is appropriate robustness and the inherent ability to withstand and perform under both cyclic and impact-type loads.

5. Current Advances in Non-Site-Welded Connection Techniques for Structures

In this review, connection systems are examined not to compare their structural strength or experimentally measured performance, but to assess their suitability for application in hybrid modular mining structures, considering constructability, tolerance sensitivity, robustness, compatibility with mining specific loading actions, and practical deployment constraints; accordingly, figures are used to support this qualitative, criteria-based synthesis rather than to enable numerical performance ranking.

5.1. Limitations of Existing Connection Techniques for Mining Structures

In the mining industry, the FEP has been popularly used for connections for stick-built and other non-volumetric structures for many decades. The FEP remains the standard connection detail for bolting structures together, and this connection type has been extensively researched and is well understood [82], as attested to by its inclusion on industry-standard detail sheets for typical stick-built structures. The need for hybrid modularisation is recognised by industry and academics alike, and specifically, the importance of an innovative, safe beam–column connection is acknowledged [22,100,101,102]. Investigations into alternative beam–column connections have been associated with higher construction efficiency and the simplification of stick-built structures, as opposed to the use of assembling prefabricated components into hybrid structures [103,104,105,106,107,108] at remote inland locations. There has also been significant work on the structural behaviour and performance of novel inter-module connections [109,110,111,112,113,114,115,116,117,118,119,120,121,122,123,124]. These connections have focused on joining full-volumetric modular structural components, with constructability and hybrid modular construction being less of a priority. Research has looked at alternatives to the standard beam–column endplate for prefabricated structures; however, the focus has been on structural integrity and seismic performance for multistorey structures [22,108,125,126,127] and has not considered typical loading conditions for mining structures.

5.2. Recent Developments of New Connection Concepts Beyond the Mining Industry

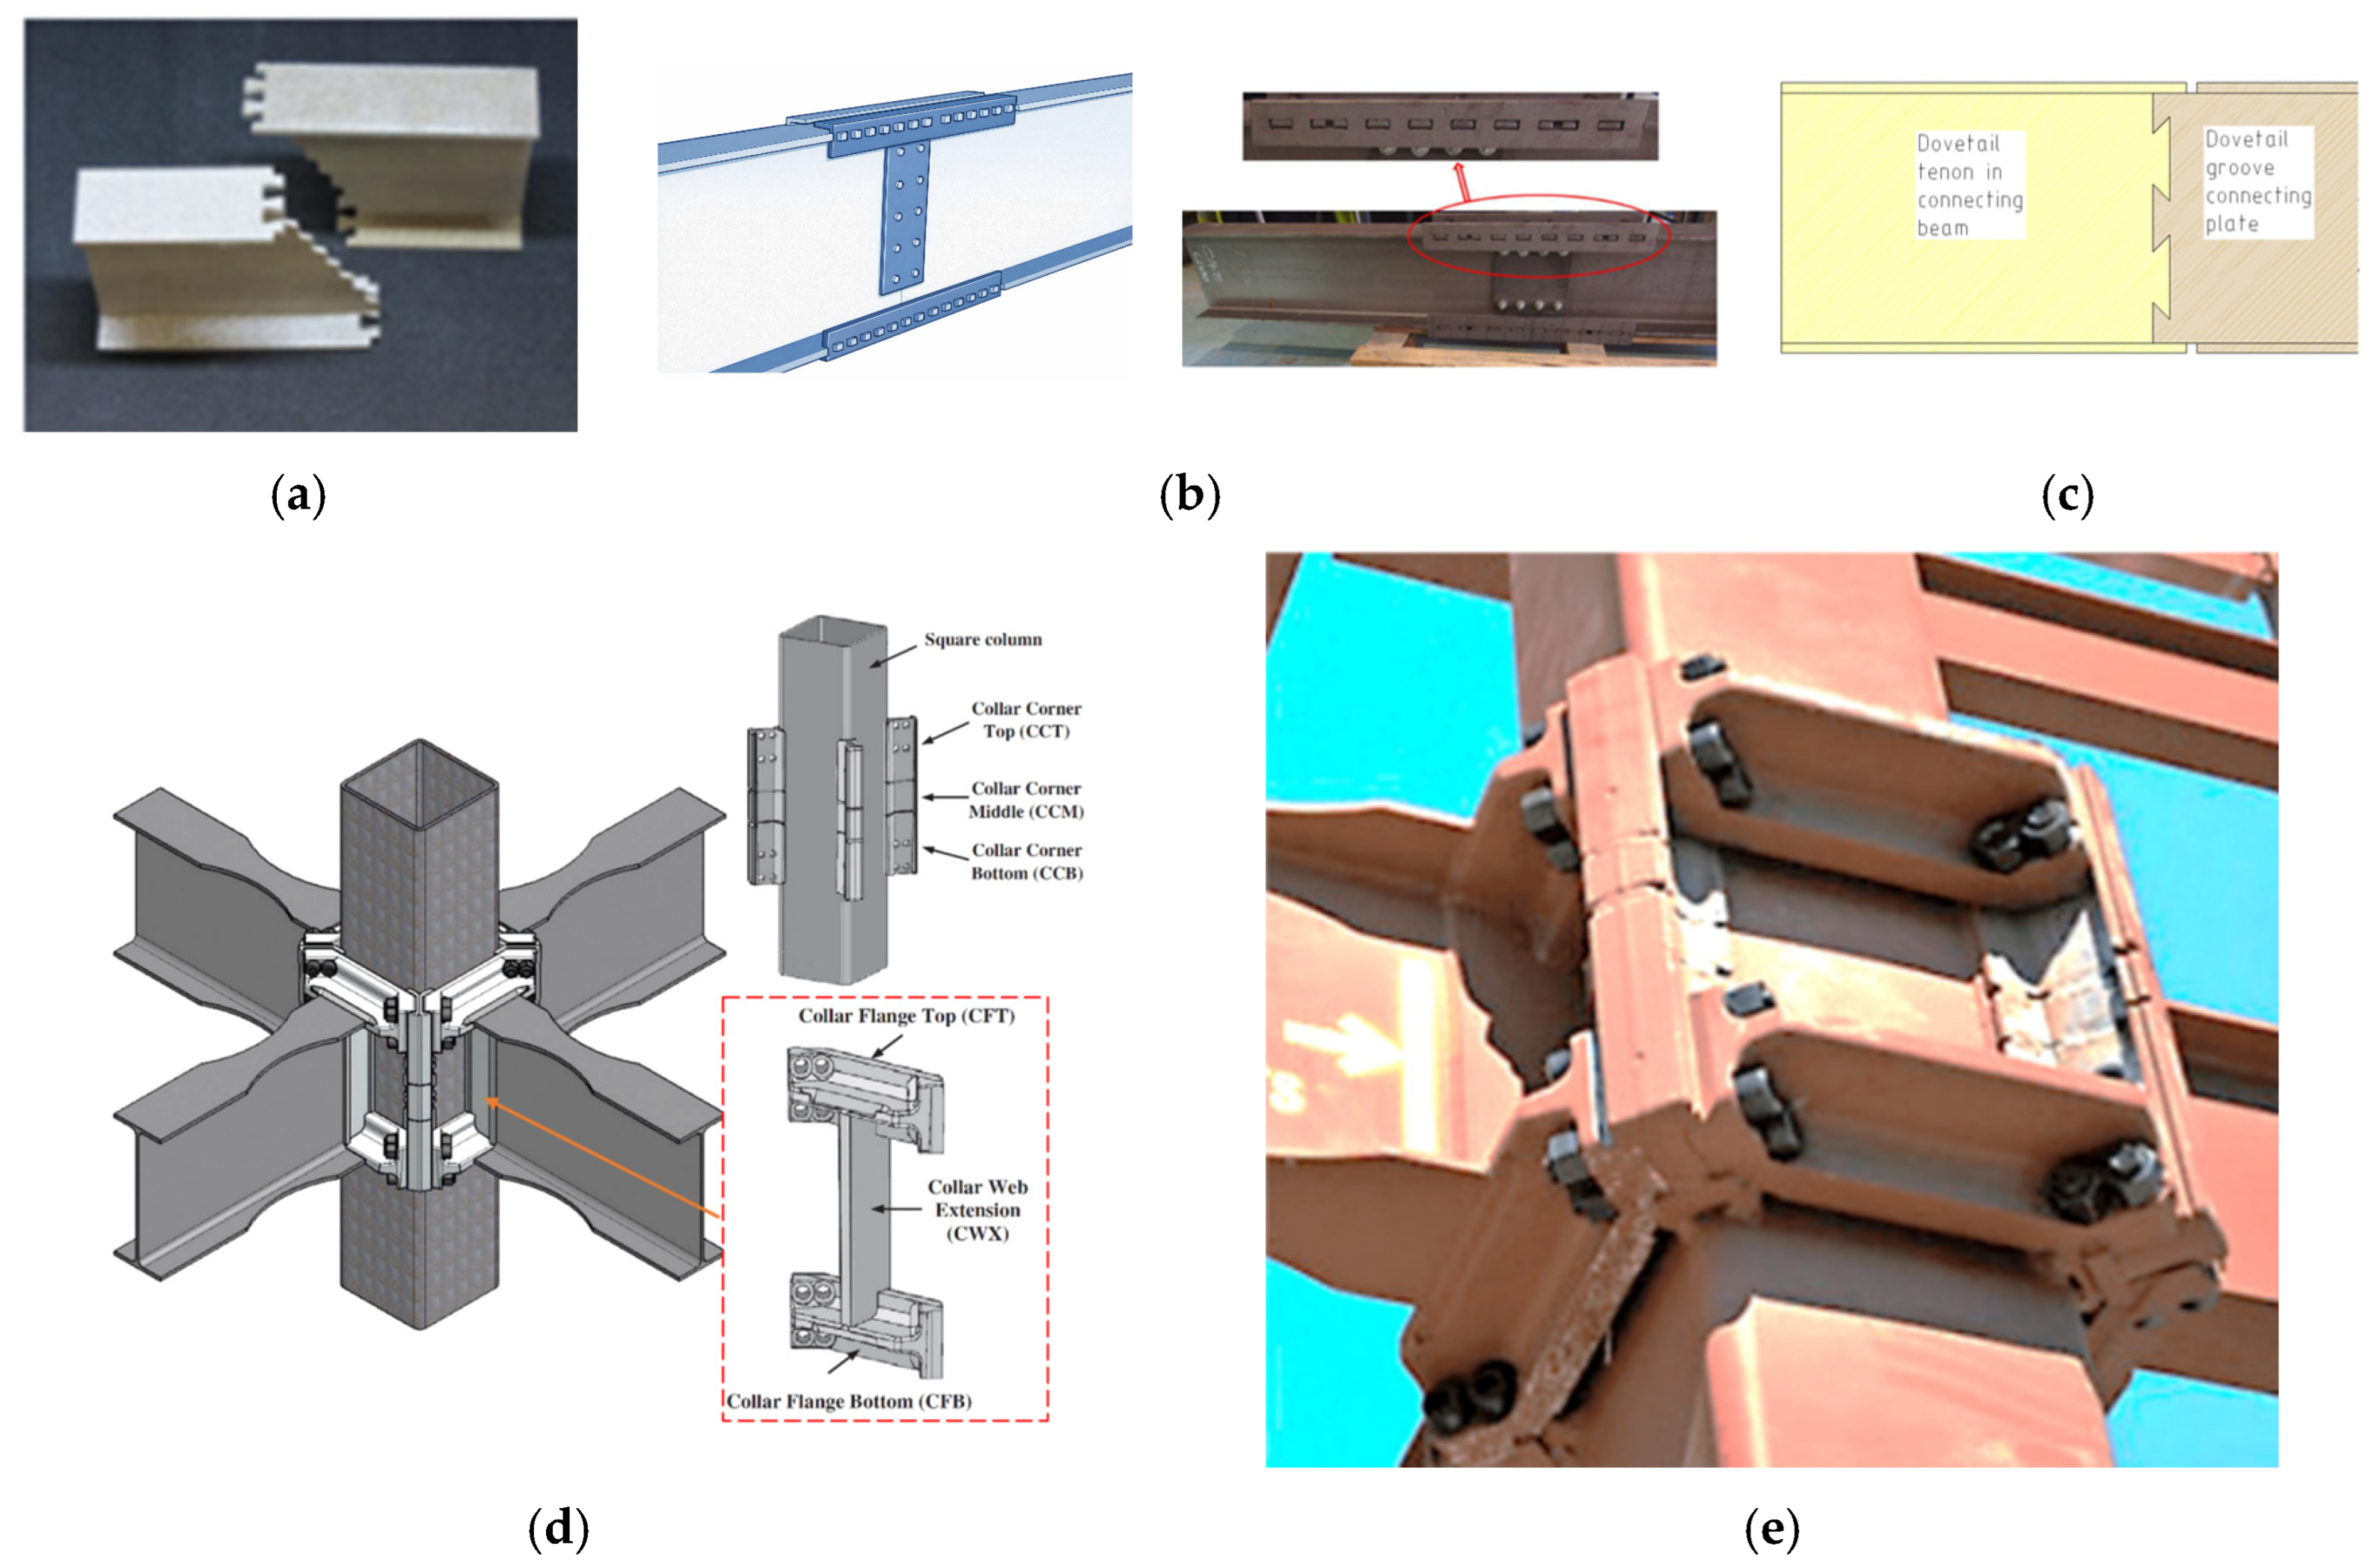
Various novel interconnecting module details have been developed [109,110,111,112,113,114,115,116,117,118,119,120,121,122,123,124,128]. However, connecting volumetric modules is different from the joining of non-volumetric prefabrication proposed here. Researchers have investigated various other alternative connections for specialist applications removed from volumetric construction, including mortice and tenon joints for external casing pipes [129], square columns to I beams [130], connections for the improvement of cyclic performance [131], connections to aid disassembly [4], connections for beam–column connections of precast structures [132], connections for improved structural performance [133], semi-rigid module connections [134], mechanical beam–column connections [135], and various other loosely related applications. Development has occurred in connections that do not rely on traditional welding and bolting techniques, and these connections provide guidance on recent developments in non-traditional connection methodology. The front-intermeshed connection was patented in 2017 [136,137], and was intended to advance construction without welding or bolting, as shown in Figure 12a. This connection detail, whilst allowing the beams to be dropped in from the top, had no self-guiding mechanism, had limited structural performance [106,107] and is suited to the point of contra-flexure for gravity loads. The connection is classified as non-ductile under both the AISC specification for structural steel buildings 2006 [138] and Eurocode 3 2005 [139]. The side-intermeshed connection (Figure 12b) is a variation on the front-intermeshed connection requiring side angles [140,141]. Whilst providing higher structural capacity, the connection has no self-guiding ability. The connection has limited applicability in the assembly of prefabricated components. The dovetail connecting plate is a mortice connection via the beam web, as shown in Figure 12c. The connection detail is engaged by a sideways sliding movement of the secondary beam [142]. There is no self-guiding mechanism, and the connection has exact tolerances. The lack of free tolerance would suggest that both ends of the beam must be slid horizontally simultaneously, which is unsuitable for the safe assembly of prefabricated components.
The ConXtech is a patented commercial system [145] with a male and female dovetail slot that is self-aligning and stable under gravity loads [105] and the components are illustrated in Figure 12d, and the assembled connection is shown in Figure 12e. The connection system has been approved under “Prequalified Connections for Special and Intermediate Steel Moment Frames for Seismic Applications” [146]. Prequalification means the connections are tested to meet the standard requirements and allow their use in seismic zones. Whilst a robust connection, ConXtech is not available for open H-section columns, and does not satisfy the constructability and tolerance requirements outlined in Section 4. These recent developments are useful, as they provide insight into the testing regimes undertaken and a valuable background to this research, though none of these proposals is directly applicable to joining prefabricated mining structures to form hybrid modules.

5.3. Insights into Prefabricated Connections with Potential Application to Hybrid Mining Structures

This section reviews recent developments in connection systems for prefabricated structures and their potential for adaptation to hybrid modular mining applications. Liu et al. [125,126] developed connections to join prefabricated components and conducted several studies, specifically targeting multi-story and high-rise structures, to verify their performance through testing and numerical analysis. The study concluded that the FEA modelling generally predicted the failure modes and that the test loading went through a number of stages, namely an elastic and then a slip stage, followed by an elastic plastic stage and then a degradation stage. Importantly, the results demonstrated the energy-absorbing capacity, extending over the full range of inter-story drift angles above those required for limit state design, indicating a robust and ductile connection. The connection, however, is labour-intensive to assemble, lacks a self-guiding mechanism, and uses box rather than H columns.
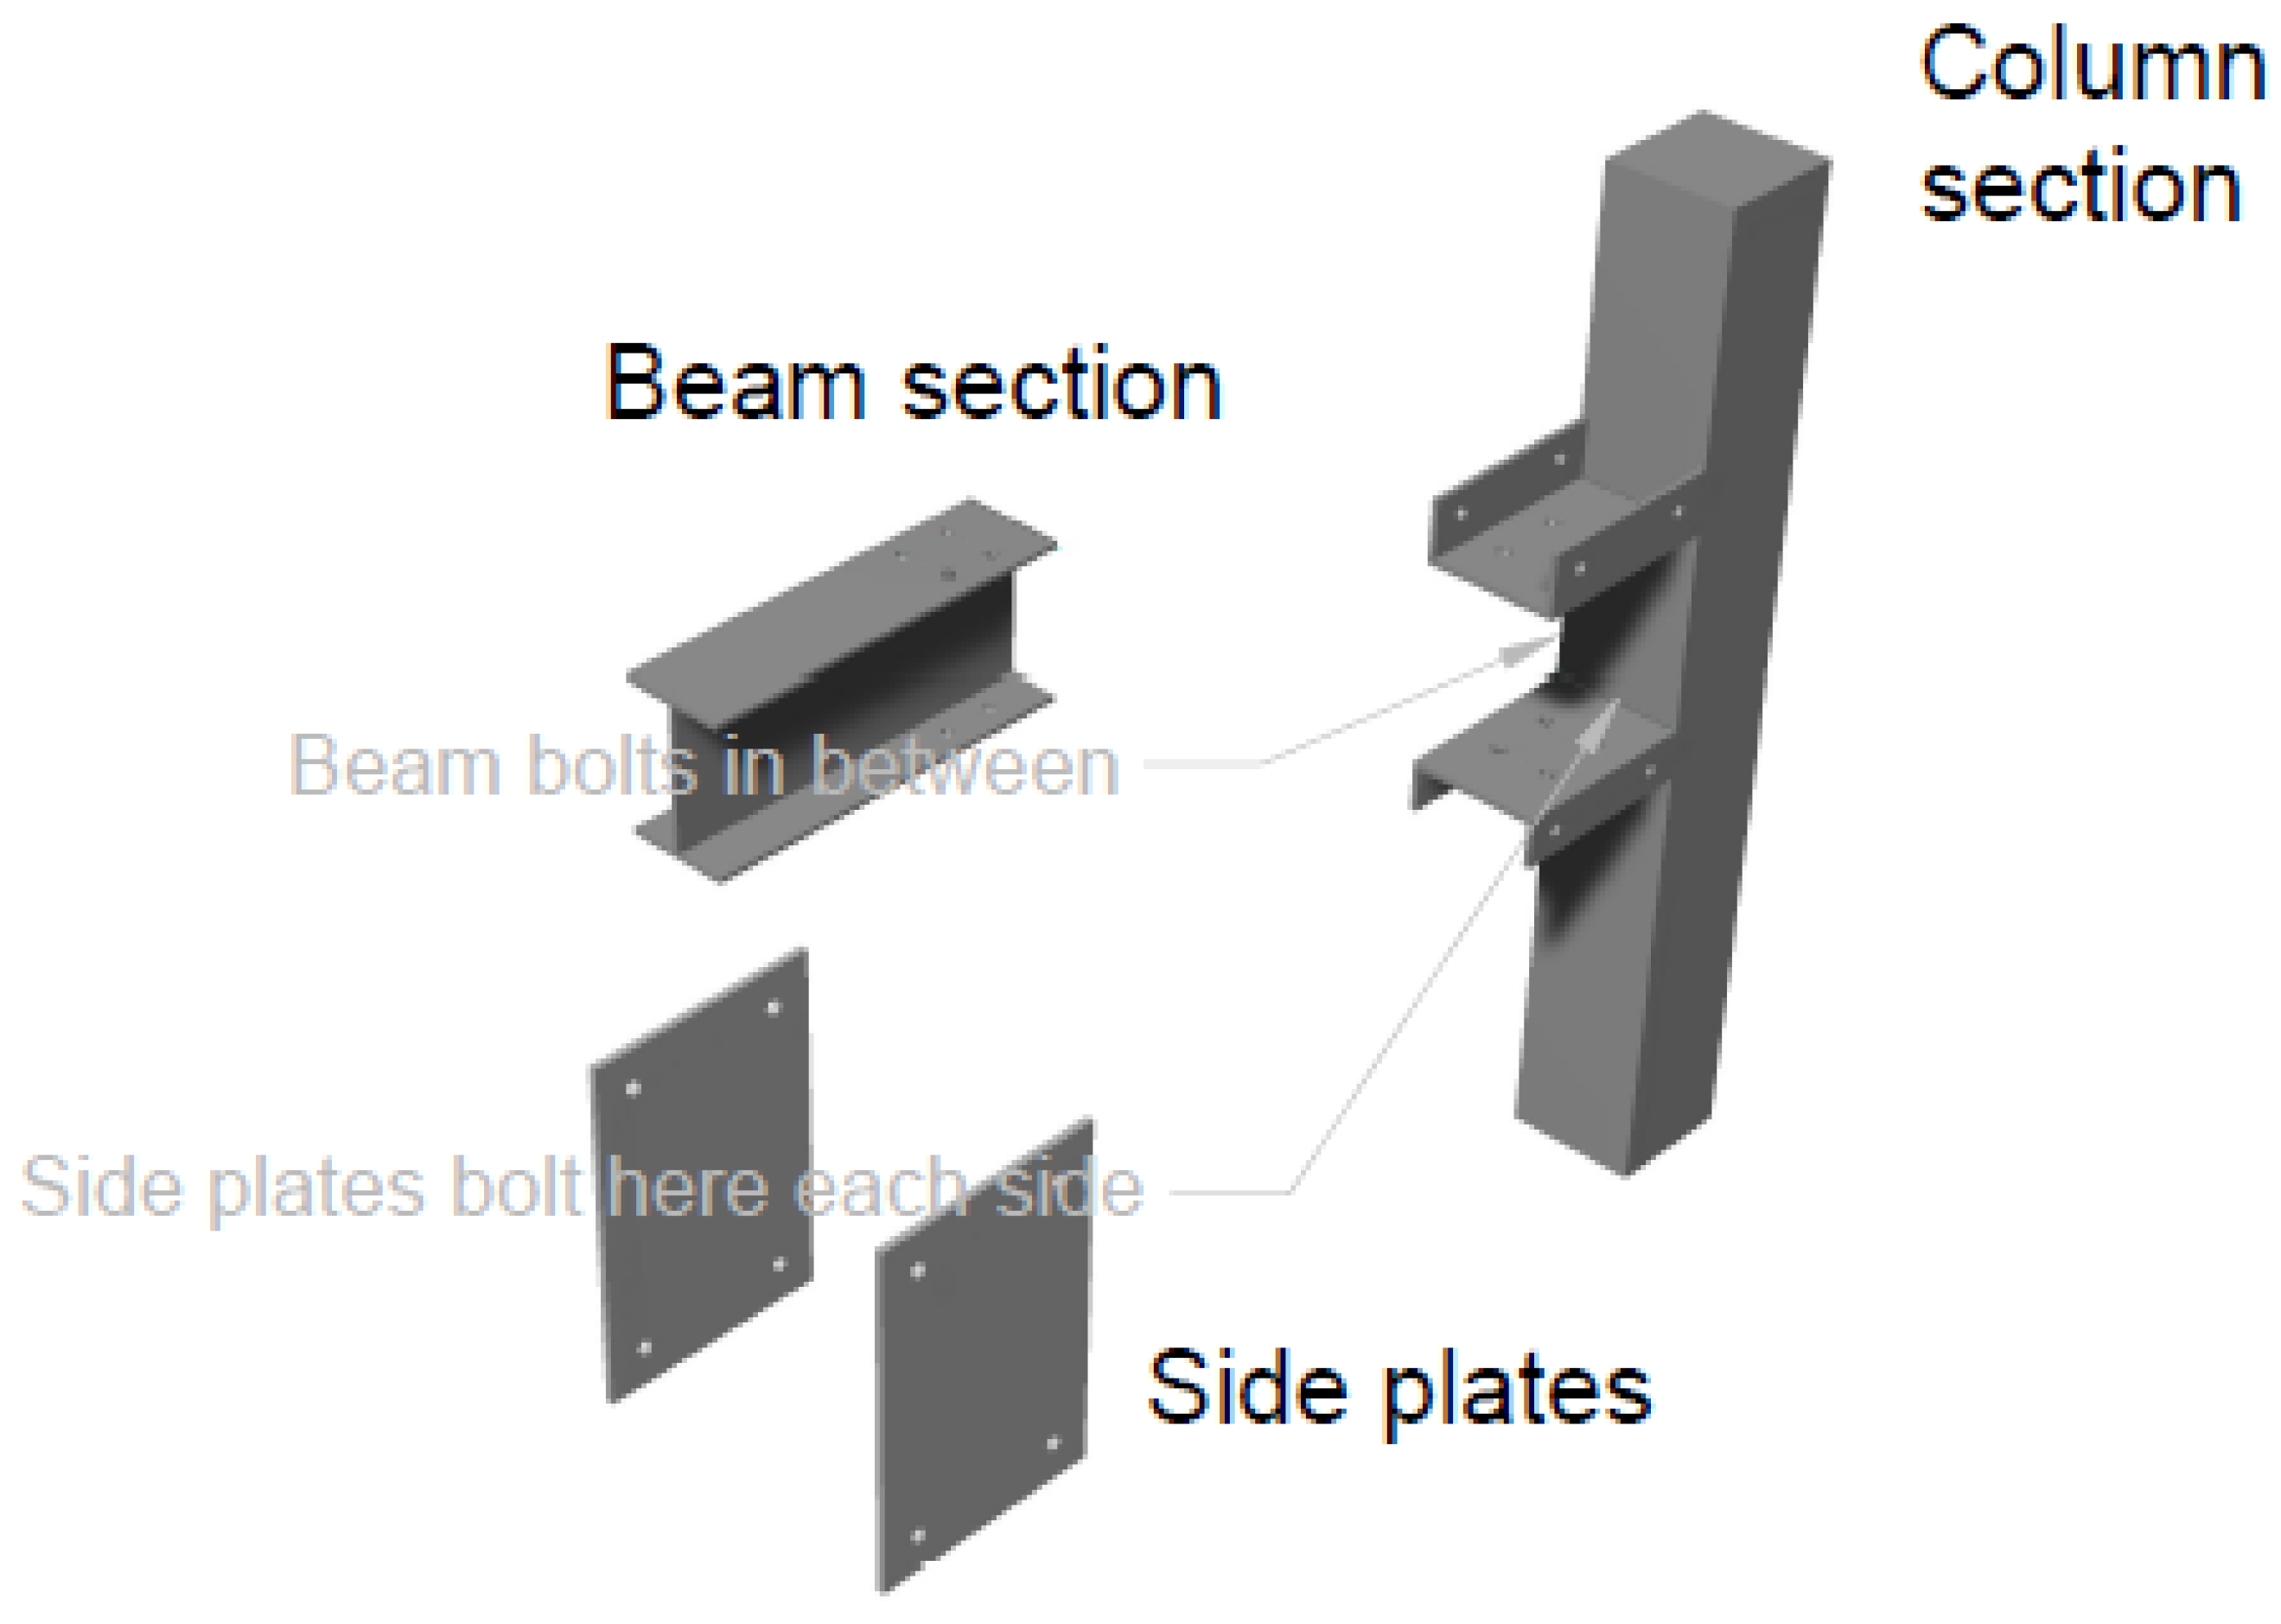
Research by Wang et al. [108] recognised the need to connect prefabrication without the need for field welding and the connection is depicted in Figure 13. The research investigated the static performance of a square tubular column with an H-shaped beam connected. The tests investigated the moment–rotation behaviour of the joint and verified the numerical models against test specimens. It was concluded that the connection reflected the expected elastic behavioural characteristics and that failure occurred by out-of-plane buckling of the beam web and slippage of the bolts, and that whilst the ultimate capacity of the joint was similar to an equivalent fully welded joint, the stiffness of this bolted joint was lower. This research is on point and relevant, providing useful insight into appropriate laboratory test regimens and the expected reduction in joint stiffness resulting from multiple potential bolt slip planes. The connection details are, however, labour-intensive to assemble and require human intervention whilst placing and bolting the components, and do not satisfy the requirements outlined in Section 4. Again, the columns are square or rectangular hollow sections and are rarely used for mining structures, and so the connection details require modification for H-shaped open column sections.
Subsequent work by Wang et al. [22] developed another beam–column joint for panelised steel modular structures, which also considered box columns and H-beam sections, and specifically examined their seismic performance. An extensive experimental investigation was undertaken to evaluate strength and stiffness, degradation under cyclic loading, rotational capacity, ductility, energy dissipation, and inter-story drift of a beam–column connection. The work also included evaluating seismic performance, and the connection followed the American Institute of Steel Construction [147] prequalification guidelines. The investigation concluded that the beam–column connection behaves semi-rigidly, allowing the incoming beam to develop its full plastic moment. The beam–column connection was found to behave in a ductile manner, with high rotational capacity, allowing storey drift angles of up to 0.09 radians and satisfying the requirements of ANSI/AISC 341-16 [148]. The test work was again undertaken with multistorey prefabricated structures in mind. Whilst this detail is not directly useful for assembling prefabricated components into hybrid modules for the mining industry, as there is no self-guiding or locking mechanism, and the detail is labour-intensive, the concept has merit for future work by being adapted by providing a self-guiding mechanism, providing construction tolerance and modifying the detail for open column sections instead of box columns.
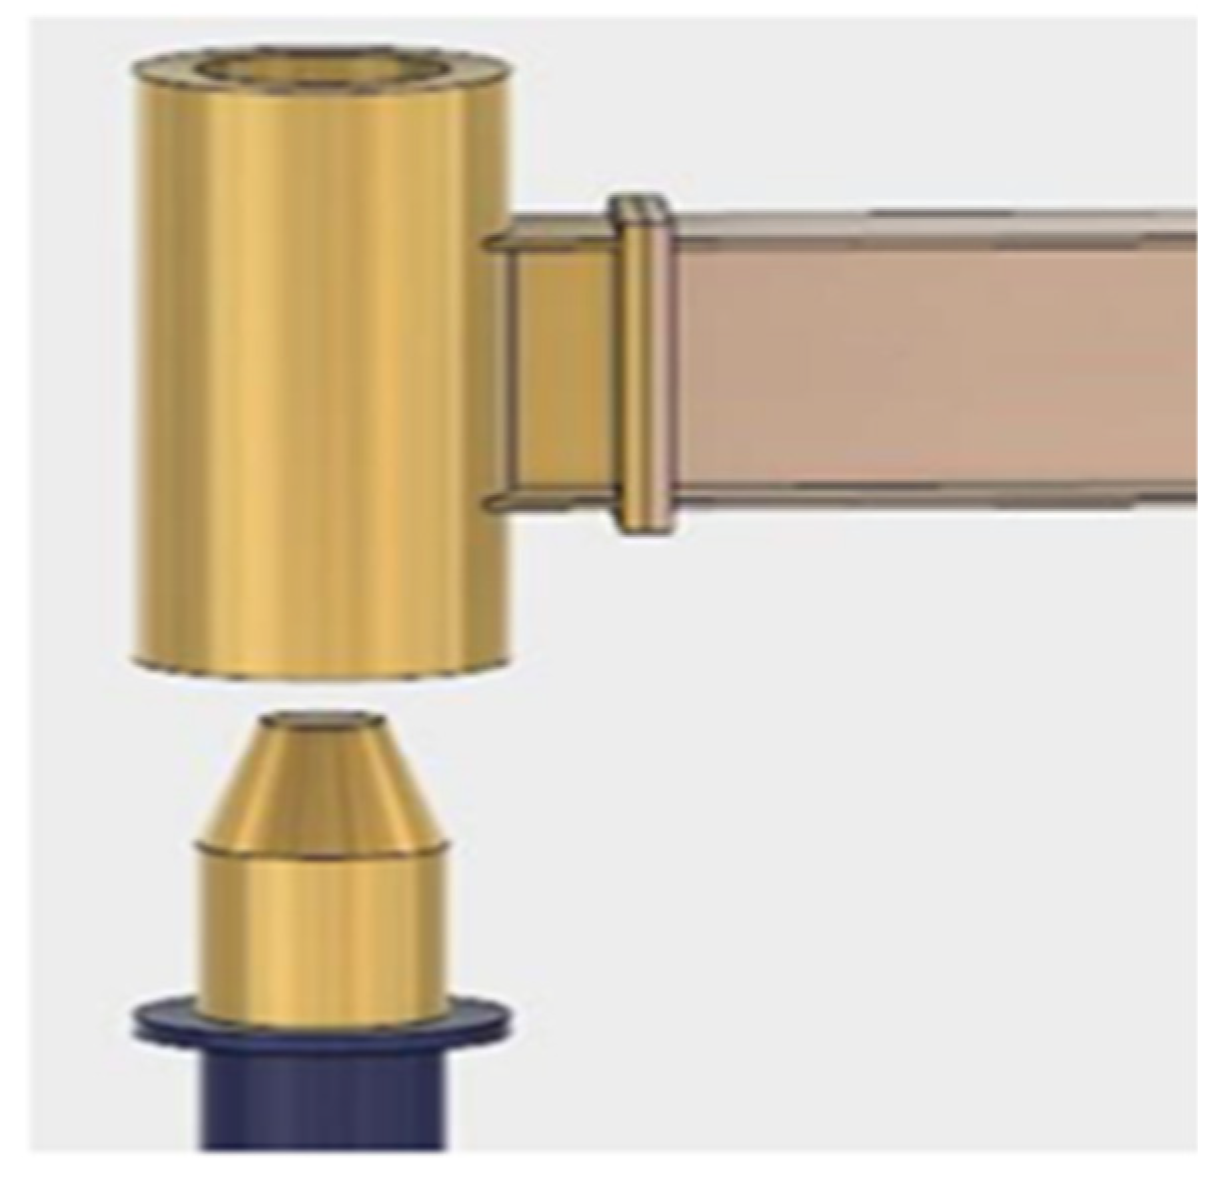
The need to reduce labour intensity from the construction site was recognised by Boulos et al. [101], who endeavoured to develop a connection that required minimal labour to install. A system utilising a spigot and socket body to join round columns and prefabricated platforms was studied, and the system is illustrated in Figure 14. The test work for this system was via scale models, utilising both a cantilever arm test and a frame test. Moment/tension interaction curves were produced for monotonic loading. The system relies solely on friction, has no bolts or field welds, and is only suitable for circular columns in its current form. Cyclic and impact testing of the connection has not been reported. The system is still under development and is intended for commercial use. It has been named AltCONNECT®, a registered trademark [101,149,150]. The system requires modification for universal column sections and requires some type of locking device to resist uplift loads; however, it is self-aligning and cognisant of construction tolerances. The AltCONNECT® is the only beam–column connection identified for use with reference to mining structures.
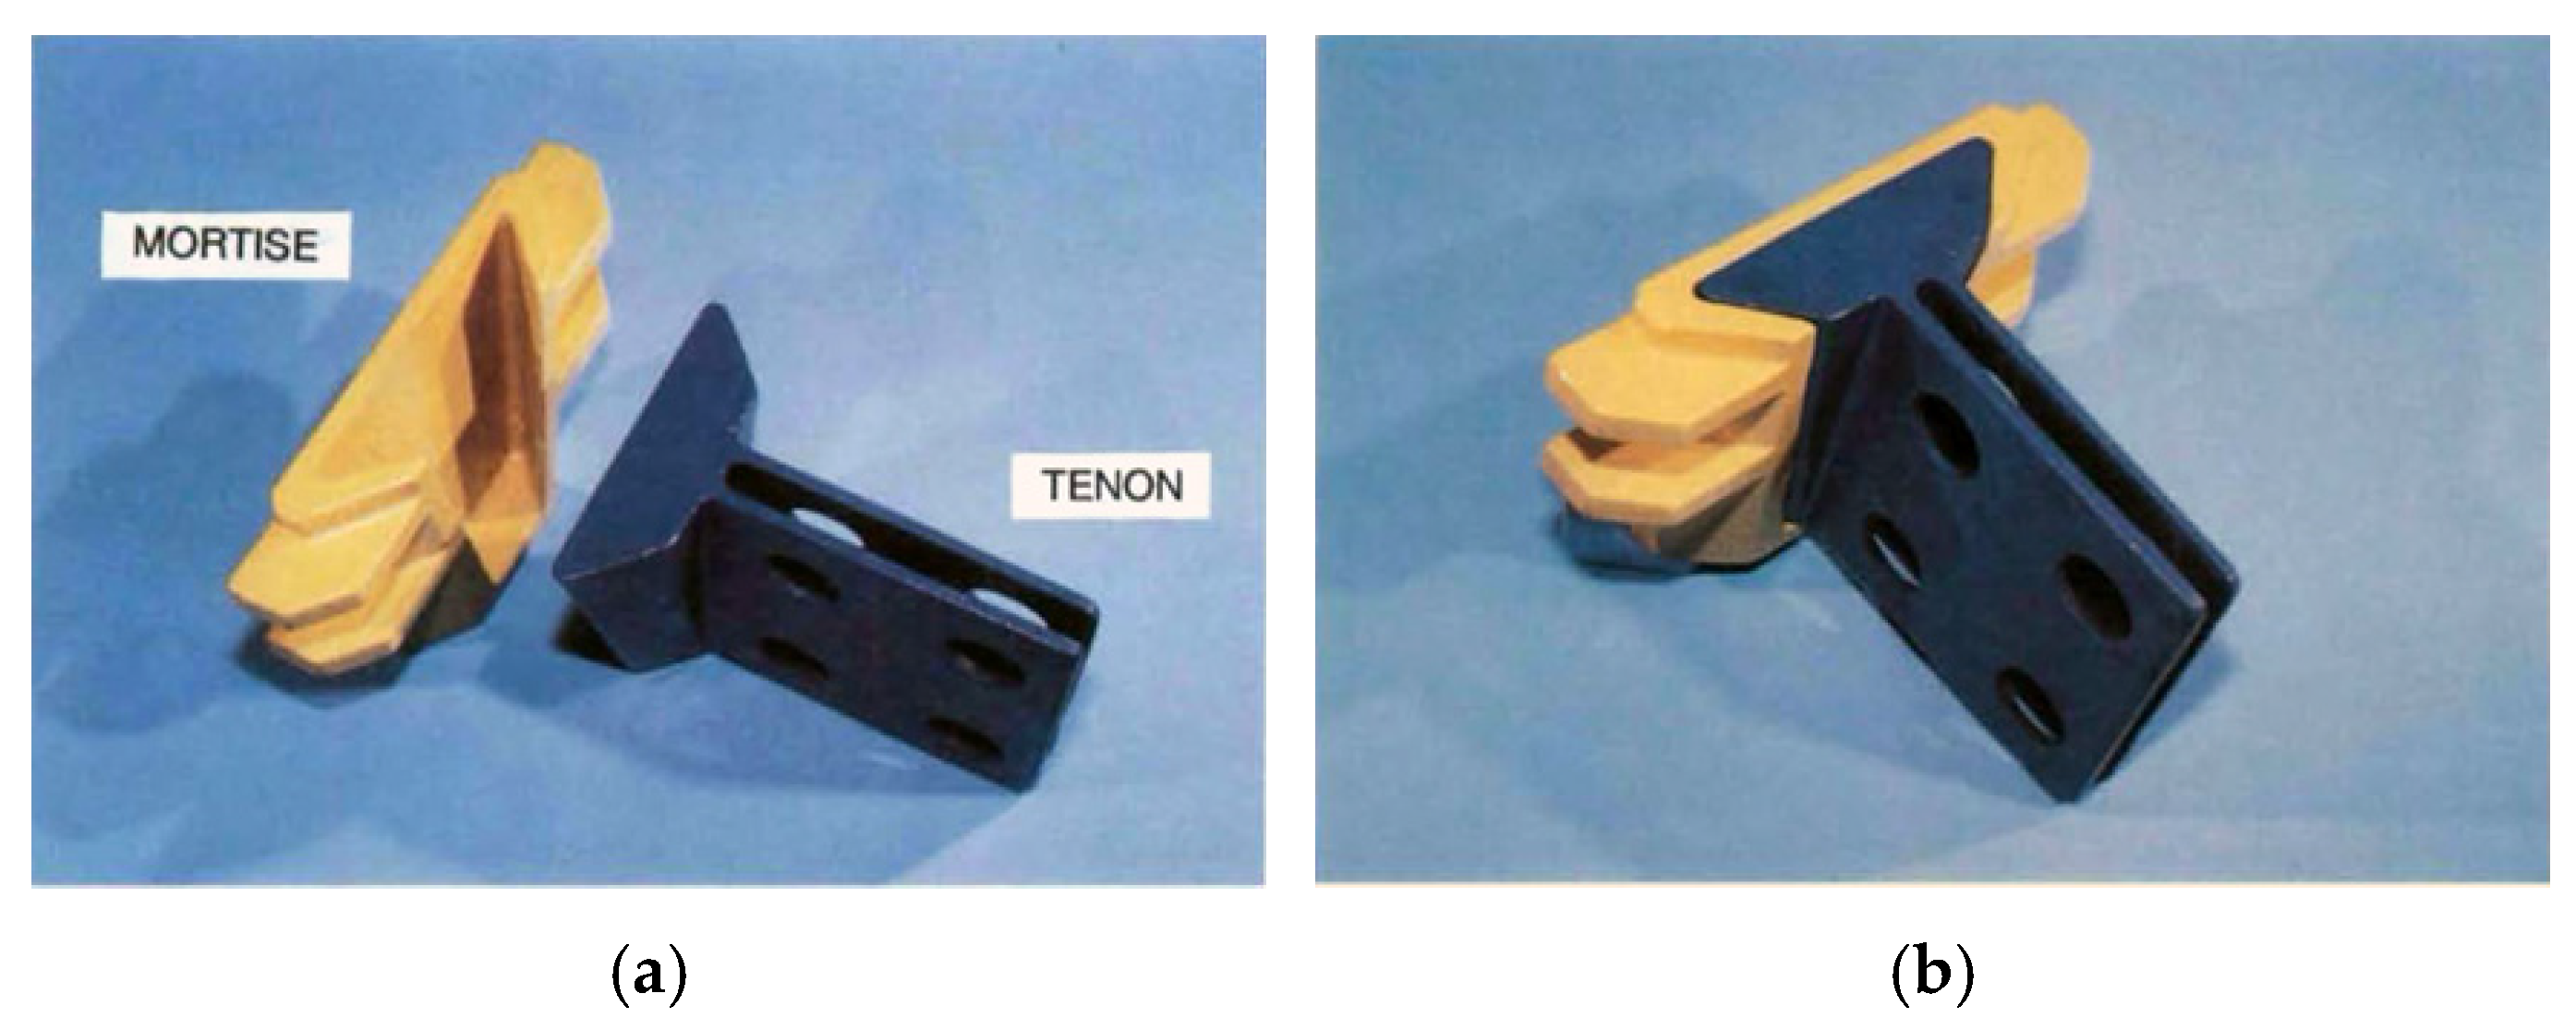
The ATLSS connection was developed to aid automated construction techniques for ordinary stick-build structures to remove the human element and speed up the erection process [104,107]. The details were not specifically designed for prefabricated components, though they are included in this review as their form is suitable for prefabricated applications. The connection comprises a mortise guide typically connected to the column and a tenon joined to the beam end. The tenon fits inside the mortise and is intended to carry shear and limited moment; see Figure 15a,b for the component parts and the assembled view. The concept was further developed to incorporate a post-erection flange plate to provide moment capacity [151]. Test regimes applied loads monotonically to obtain load-deflection curves and as cyclic loads following a seismic program developed in 1983 [151]. The ATLSS concept was commercially developed in the 1990s but has not gained widespread acceptance. This connection detail satisfies several key requirements outlined in Section 4 for mining structures. Its biggest drawbacks are the inability to resist upward loads, inherent robustness, and limited construction tolerance, though each could be overcome with further development.

5.4. The Ideal Beam–Column Connection for Hybrid Structures

A review of the current literature indicates that, while there are many novel beam–column connections, no existing concepts directly suitable for assembling prefabricated end frame and panel components into hybrid modular structures have been identified. The investigations and studies reviewed in this paper generally centre around high-rise and commercial structures. Test work and laboratory test procedures in these studies variously investigate both monotonic and cyclic loading. Cyclic tests investigate seismic response, and cyclic loading is generally considered [153] under the ATC [154] and SAC protocols [155], whilst mining structures are subject to cyclic operational loads as well. The work in these studies has demonstrated test setups that allow connection behaviour to be tested and understood for a limited set of loading cases. Whilst these loading regimes are applicable to novel beam–column connections for mining structures, the testing regime must be extended to include the various transient and operational loads defined in Section 2. to which mining structures are subjected, and which are generally designed to accommodate.
There are several shortcomings observed in existing approaches, including (1) a lack of self-guiding or self-locking ability, (2) difficulties caused by construction tolerances that prevent components from sliding down into position between fixed columns, (3) inadequate structural robustness and strength, and (4) an inability to be structurally stable once placed before further human interaction, which have been summarised in [1]. The ideal solution for a beam–column connection for hybrid structures would satisfy all these key requirements.

6. Conclusions and Future Perspectives

Volumetric prefabrication offers a sustainable and efficient approach to construction, both generally and specifically for Australian remote mine sites. Remote locations present unique obstacles that preclude full volumetric construction in all instances. Logistical transport challenges restrict the volumetric size and weight. There are transport restrictions due to existing infrastructure that have never been considered for transporting large volumetric construction. Innovative hybrid modular solutions offer a means to overcome the logistical challenges associated with transport in contexts where volumetric construction is impractical. Such a hybrid approach can maximise benefits from prefabrication for inland industrial and mining projects. The following conclusions are drawn from this study.
  • Mining structures are subjected to the common structural hazards of gravity and environmental loads as outlined in the various loading codes. In addition, mining structures are subjected to operational loads from machinery and vehicles, as well as to impacts. Volumetric construction involves additional lifting, SPMT transport, ocean and sea forces, and road transport loads. Therefore, mining structures must adequately perform and respond to the loadings in addition to normal building structures. Connection details for mining structures must be resilient and capable of responding to and resisting the demands imposed by these additional hazards. The mining industry currently relies on the FEP for beam–column connections; however, it is not well-suited for hybrid modular structures. There is a need to develop new types of connections to facilitate the fast joining and erection of prefabricated components.
  • In the Australian mining industry, suitable beam–column connections would allow efficient connection of prefabricated frames and panels, which could be used to facilitate hybrid modular construction. None of the existing beam–column connections satisfied the installation criteria identified in this paper.
  • Developing new beam–column connection that performs resiliently in response to imposed hazards and meets the above construction requirements is essential. Such development will enable the mining industry to safely and efficiently connect transportable-sized prefabricated components into hybrid modular structures.
The synthesis presented in this review highlights that future research on modular mining process structures should move beyond adapting connection systems developed for commercial and high-rise buildings. Priority should be given to connection concepts that explicitly address erection safety, tolerance accommodation, and stability of partially completed structures, as well as experimental validation under mining-specific operational and transient loading conditions. Establishing test protocols and design strategies aligned with these requirements is a critical step toward enabling safe, robust hybrid modular construction in remote mining environments.

Author Contributions

P.J.K.: Conceptualisation, Investigation, Writing—original draft. A.W.L.: Supervision, Conceptualisation, Validation, Writing—review and editing. W.C.: Funding acquisition, Supervision, Conceptualisation, Validation, Writing—review and editing. H.H.: Supervision, Writing—review and editing. All authors have read and agreed to the published version of the manuscript.

Funding

This research was funded by the Australian Research Council (ARC) Future Fellowship grant number FT210100050.

Data Availability Statement

No new data were created or analysed in this study.

Acknowledgments

The first author acknowledges the support received through the Australian Government Research Training Program Scholarship. The authors acknowledge the financial support from the Australian Government through the Australian Research Council (ARC) Future Fellowship (FT210100050).

Conflicts of Interest

The authors declare no conflicts of interest.

References

  1. Kreppold, P.J.; Lacey, A.W.; Hao, H.; Chen, W. Review of prefabrication and volumetric mining structures: Current practice, challenges, and future prospects. Structures 2025, 79, 109506. [Google Scholar] [CrossRef] [Scilit]
  2. Jiang, Y.; Zhao, D.; Wang, D.; Xing, Y. Sustainable Performance of Buildings through Modular Prefabrication in the Construction Phase: A Comparative Study. Sustainability 2019, 11, 5658. [Google Scholar] [CrossRef] [Scilit]
  3. Huang, Z.; Zhou, H.; Tang, H.; Zhao, Y.; Lin, B. Carbon Emissions of Prefabricated Steel Structure Components: A Case Study in China. J. Clean. Prod. 2023, 406, 137047. [Google Scholar] [CrossRef] [Scilit]
  4. O’Grady, T.M.; Minunno, R.; Chong, H.-Y.; Morrison, G.M. Interconnections: An Analysis of Disassemblable Building Connection Systems Towards a Circular Economy. Buildings 2021, 11, 535. [Google Scholar] [CrossRef] [Scilit]
  5. Li, Z.; Shen, G.Q.; Alshawi, M. Measuring the Impact of Prefabrication on Construction Waste Reduction: An Empirical Study in China. Resour. Conserv. Recycl. 2014, 91, 27–39. [Google Scholar] [CrossRef] [Scilit]
  6. Hu, R.; Chen, K.; Fang, W.; Zheng, L.; Xu, J. The Technology-Environment Relationship Revisited: Evidence from the Impact of Prefabrication on Reducing Construction Waste. J. Clean. Prod. 2022, 341, 130883. [Google Scholar] [CrossRef] [Scilit]
  7. Chippagiri, R.; Bras, A.; Sharma, D.; Ralegaonkar, R.V. Technological and Sustainable Perception on the Advancements of Prefabrication in Construction Industry. Energies 2022, 15, 7548. [Google Scholar] [CrossRef] [Scilit]
  8. Jaillon, L.; Poon, C.S.; Chiang, Y.H. Quantifying the Waste Reduction Potential of Using Prefabrication in Building Construction in Hong Kong. Waste Manag. 2009, 29, 309–320. [Google Scholar] [CrossRef] [Scilit] [PubMed]
  9. Jeong, J.; Hong, T.; Ji, C.; Kim, J.; Lee, M.; Jeong, K.; Lee, S. An Integrated Evaluation of Productivity, Cost and CO2 Emission between Prefabricated and Conventional Columns. J. Clean. Prod. 2017, 142, 2393–2406. [Google Scholar] [CrossRef] [Scilit]
  10. Cao, X.; Li, X.; Zhu, Y.; Zhang, Z. A Comparative Study of Environmental Performance between Prefabricated and Traditional Residential Buildings in China. J. Clean. Prod. 2015, 109, 131–143. [Google Scholar] [CrossRef] [Scilit]
  11. Pervez, H.; Ali, Y.; Petrillo, A. A Quantitative Assessment of Greenhouse Gas (GHG) Emissions from Conventional and Modular Construction: A case of developing country. J. Clean. Prod. 2021, 294, 126210. [Google Scholar] [CrossRef] [Scilit]
  12. Walker, S. Making the Most of Modules. Eng. Min. J. 2016, 217, 26. [Google Scholar]
  13. Storey, K. Fly-in/Fly-Out: Implications for Community Sustainability. Sustainability 2010, 2, 1161–1181. [Google Scholar] [CrossRef] [Scilit]
  14. Storey, K. Fly-in/Fly-out and Fly-over: Mining and Regional Development in Western Australia. Aust. Geogr. 2001, 32, 133–148. [Google Scholar] [CrossRef]
  15. Parliament of Australia. Inquiry into the Use of ‘Fly-In, Fly-Out’ (Fifo) Workforce Practices in Regional Australia; Australia HoRSCoR, Ed.; Parliament of Australia: Canberra, Australia, 2012. [Google Scholar]
  16. McKenzie, F.; Haslam Mckenzie, F.; Hoath, A. Fly-In/Fly-Out, Flexibility and the Future: Does Becoming a Regional FIFO Source Community Present Opportunity or Burden? Geogr. Res. 2014, 52, 430–441. [Google Scholar] [CrossRef] [Scilit]
  17. Deacon, L.; Papineau, J.W.; Lamanes, T. Transiency, Fly-in-Fly-out Workers, and Sustainability: Perceptions from within a Resource-Based Community. WIT Trans. Ecol. Environ. 2018, 226, 95–105. [Google Scholar] [CrossRef] [Scilit]
  18. Caulfield, J. Skilled Labor Shortages Continue to Make Off-Site Fabrication and Construction Attractive. Building Design & Construction. 10 January 2019. Available online: https://www.bdcnetwork.com/home/news/55162233/skilled-labor-shortages-continue-to-make-off-site-fabrication-and-construction-attractive (accessed on 5 December 2024).
  19. Jones, A.G. Mining for Net Zero; the Impossible Task. Lead. Edge 2023, 42, 266–276. [Google Scholar] [CrossRef] [Scilit]
  20. International Energy Agency. The Role of Critical Minerals in Clean Energy Transitions; OECD: Paris, France, 2021. [Google Scholar] [CrossRef] [Scilit]
  21. Wu, Z.; Luo, L.; Li, H.; Wang, Y.; Bi, G.; Antwi-Afari, M.F. An Analysis on Promoting Prefabrication Implementation in Construction Industry Towards Sustainability. Int. J. Environ. Res. Public Health 2021, 18, 11493. [Google Scholar] [CrossRef] [Scilit]
  22. Wang, H.; Zhao, X.; Ma, G. Experimental Study on Seismic Performance of Column-column-beam Joint in Panelised Steel-Modular Structure. J. Constr. Steel Res. 2022, 192, 107240. [Google Scholar] [CrossRef] [Scilit]
  23. Geoscience, Australia. Critical Minerals at Geoscience Australia; Geoscience Australia: Canberra, Australia, 2023.
  24. Caritat, P.; Mcinnes, B.; Walker, A.; Bastrakov, E.; Rowins, S.; Prent, A. The Heavy Mineral Map of Australia: Vision and Pilot Project. Minerals 2022, 12, 961. [Google Scholar] [CrossRef] [Scilit]
  25. O’connor, J.T.; O’brien, W.J.; Choi, J.O. Industrial Project Execution Planning: Modularization Versus Stick-Built. Pract. Period. Struct. Des. Constr. 2016, 21, 04015014. [Google Scholar] [CrossRef] [Scilit]
  26. Gill, J.C.; Malamud, B.D. Reviewing and Visualizing the Interactions of Natural Hazards. Rev. Geophys. 2014, 52, 680–722. [Google Scholar] [CrossRef] [Scilit]
  27. Gill, J.C.; Malamud, B.D. Hazard Interactions and Interaction Networks (Cascades) within Multi-Hazard Methodologies. Earth Syst. Dyn. 2016, 7, 659–679. [Google Scholar] [CrossRef] [Scilit]
  28. Lacey, A.W.; Chen, W.; Hao, H.; Bi, K. Structural Response of Modular Buildings—An Overview. J. Build. Eng. 2018, 16, 45–56. [Google Scholar] [CrossRef] [Scilit]
  29. Gardoni, P.; Lafave, J.M. Multi-Hazard Approaches to Civil Infrastructure Engineering: Mitigating Risks and Promoting Resilence; Springer: Cham, Switzerland, 2016. [Google Scholar] [CrossRef] [Scilit]
  30. AS/NZS 1594:2025; Hot-Rolled Steel Flat Products. SAI Global Limited: Sydney, Australia, 2025.
  31. American Society of Civil E. Minimum Design Loads and Associated Criteria for Buildings and Other Structures; American Society of Civil Engineers: Reston, VA, USA, 2017. [Google Scholar]
  32. EN 1990:2002; Basis of Structural Design. European Committee for Standardization (CEN): Brussels, Belgium, 2002.
  33. Monash University. Handbook for the Design of Modular Structures; Monash University: Melbourne, Australia, 2017. [Google Scholar]
  34. BHP Iron Ore Pty Ltd. WAIO Standard—Design Criteria—Structures; Wanke, L., Ed.; BHP Iron Ore Pty Ltd.: Perth, Western Australia, 2021. [Google Scholar]
  35. AS 1170.1:2002; Structural Design Actions. Part 1 Permanant Imposed and Other Actions. SAI Global Limited: Sydney, Australia, 2002.
  36. EN 1991-4:2006; Actions on Structures—Part 4: Silos and Tanks. European Committee for Standardization (CEN): Brussels, Belgium, 2006.
  37. Kamari, A.; Bartlomiej Marek, K.; Schultz, C.P.L. A Bim-Based Lca Tool for Sustainable Building Design During the Early Design Stage. Smart Sustain. Built Environ. 2022, 11, 217–244. [Google Scholar] [CrossRef] [Scilit]
  38. AS 3774-1996; Loads on Bulk Solids Containers. SAI Global Limited: Sydney, Australia, 1996.
  39. Fank, M.Z.; Nascimento, J.W.B.; Cardoso, D.L.; Meira, A.S.; Willrich, F.L. Vertical Pressures and Compressive Friction Force in a Large Silo. Eng. Agrícola 2018, 38, 498–503. [Google Scholar] [CrossRef] [Scilit]
  40. Morgan, R.; Bird, W.; Zhu, F.; Go, G. Investigation of revised AS 4324.1 partial load factors for steel bulk materials handling structures. Aust. J. Struct. Eng. 2017, 18, 224–232. [Google Scholar] [CrossRef] [Scilit]
  41. AS 1170.4:2007; Structural Design Actions. Part 4 Earthquake Actions in Australia. SAI Global Limited: Sydney, Australia, 2007.
  42. AT Mineral Processing. When is a Conveyor Upgrade Actually a Downgrade? 2024. Available online: https://www.at-minerals.com/imgs/2/0/3/2/0/3/9/05_Aggreagate_Spillage_Discharge_300dpi_3500x2625_-898cd2690cf9c97d.jpeg (accessed on 18 June 2024).
  43. Holmes, J. Tropical Cyclone impacts on the Western Australian Coast and Extreme Wind Speeds in Region D. Aust. J. Struct. Eng. 2021, 22, 110–119. [Google Scholar] [CrossRef] [Scilit]
  44. AS 1170.2:2021; Structural Design Actions. Part 2 Wind Actions. SAI Global Limited: Sydney, Australia, 2021.
  45. HB 212-2002; Design Wind Speeds for the Asia-Pacific Region. Standards Australia International: Sydney, Australia, 2002.
  46. EN 1991-1-4:2005; Actions on Structures—Part 1-4: General Actions—Wind Actions. European Committee for Standardization (CEN): Brussels, Belgium, 2005.
  47. EN 1991-1-2:2002; Actions on Structures—Part 1-2: General Actions—Actions on Structures Exposed to Fire. European Committee for Standardization (CEN): Brussels, Belgium, 2002.
  48. EN 1993-1-2:2005; Design of Steel Structures—Part 1-2: General Rules Structural Fire Design. European Committee for Standardization (CEN): Brussels, Belgium, 2005.
  49. Alasiri, M.R.; Mahamid, M. A Comparison between Cfd and Thermal-Structural Analysis of Structural Steel Members Subjected to Fire. J. Struct. Fire Eng. 2021, 12, 234–255. [Google Scholar] [CrossRef] [Scilit]
  50. Maraveas, C.; Fasoulakis, Z.C.; Tsavdaridis, K.D. Mechanical properties of High and Very High Steel at elevated temperatures and after cooling down. Fire Sci. Rev. 2017, 6, 3. [Google Scholar] [CrossRef] [Scilit]
  51. Huang, L.; Li, G.Q.; Wang, X.X.; Zhang, C.; Choe, L.; Engelhardt, M. High Temperature Mechanical Properties of High Strength Structural Steels Q550, Q690 and Q890. Fire Technol. 2018, 54, 1609–1628. [Google Scholar] [CrossRef] [Scilit]
  52. Naser, J.; Alam, F.; Khan, M. Evaluation of a Proposed Dust Ventilation/Collection System in an Underground Mine Crushing Plant. WSEAS Trans. Fluid Mech. 2008, 3, 244–249. [Google Scholar] [CrossRef]
  53. KIS Plant Pty Ltd. KIS Hopper Feed Bins. 2021. Available online: https://kisplant.com.au/news-detail.php?Full-steam-ahead-at-Bromelton-Quarry-1 (accessed on 18 April 2026).
  54. Reed, W.; Colinet, J.; Fox, W.R.; Franta, R.J.; Joy, G.; Pesser, P.W.; Rounds, J.R.; Schultz, M.J. Dust Control Handbook for Industrial Minerals Mining and Processing RI 9689 REPORT OF INVESTIGATIONS/2012 Chapter 3: Drilling and Blasting. In Dust Control Handbook for Industrial Minerals Mining and Processing RI9689 Report of Investigations; Department of Health and Human Services, Centers for Disease Control and Prevention, National Institute for Occupational Safety and Health: Washington, DC, USA, 2012; pp. 70–108. [Google Scholar]
  55. McLanahan. How to Size a Jaw Crusher. 23 June 2023. Available online: https://mclanahan.com/blog/how-to-size-a-jaw-crusher (accessed on 3 April 2024).
  56. Duff, E.; Caris, C.; Bonchis, A.; Taylor, K.; Gunn, C.; Adcock, M. The Development of a Telerobotic Rock Breaker. In Field and Service Robotics; Springer: Berlin/Heidelberg, Germany, 2009; pp. 411–420. Available online: https://link.springer.com/chapter/10.1007/978-3-642-13408-1_37 (accessed on 9 April 2024).
  57. Creighton Rock Drill Ltd. Stationary Rockbreaker Applications. 2024. Available online: https://www.crdcreighton.com/products/aggregates/astec-rockbreaker-systems/rockbreaker-applications/ (accessed on 9 April 2024).
  58. Mineral Processing Solutions. Fixed Rockbreaker Boom Systems; Mineral Processing Solutions: Bibra Lake, Australia, 2024. [Google Scholar]
  59. Szczerbakowicz, M.; Suchorab, N.; Król, R. Preliminary Failure Frequency Analysis of Receiving Bins in Retention Bunkers Operated in Underground Copper Ore Mines. Appl. Sci. 2021, 11, 3628. [Google Scholar] [CrossRef] [Scilit]
  60. Roark, R.J.; Romain, J.E. Formulas for Stress and Strain, International ed.; McGraw-Hill: New York, NY, USA, 1986. [Google Scholar]
  61. Nagpal, S.; Jain, N.; Sanyal, S. Stress Concentration and Its Mitigation Techniques in Flat Plate with Singularities—A Critical Review. Eng. J. 2012, 16, 1–16. [Google Scholar] [CrossRef] [Scilit]
  62. Hua, X. Design of Pipe Racks Using Pre-Assembled Units or Modules. In Structures Congress 2014; ASCE: Reston, VA, USA, 2014; pp. 1638–1651. [Google Scholar] [CrossRef] [Scilit]
  63. Lei, Z.; Al-Hussein, M.; Hermann, U.; Bouferguene, A. Heavy Lift Analysis at Feed Stage for Industrial Project. In 2016 Winter Simulation Conference (WSC); IEEE: New York, NY, USA, 2016; pp. 3281–3289. [Google Scholar] [CrossRef] [Scilit]
  64. AS 1418.1:2021; Cranes, Hoists and Winches, Part 1: General Requirements. SAI Global Limited: Sydney, Australia, 2021.
  65. AS 5221.1:2021; Cranes—Design Principles for Loads and Load Combinations, Part 1: General (ISO8686-1:2012,MOD). SAI Global Limited: Sydney, Australia, 2021.
  66. Blodgett, O.W. Design of Welded Structures: The James F Lincoln Arc Welding Foundation; James F. Lincoln Arc Welding Foundation: Cleveland, OH, USA, 1966. [Google Scholar]
  67. AS 4991-2004; Lifting Devices. SAI Global Limited: Sydney, Australia, 2004.
  68. Roy, S.P. Consider Modular Plant Design. Chem. Eng. Prog. 2017, 113, 28–31. [Google Scholar]
  69. Dorafshan, S.; Maguire, M.; Culmo, M.P.; Dorafshan, S.; Maguire, M.; Halling, M.W.; Barr, P.J.; Culmo, M.P. Dynamic Effects Caused by SPMT Bridge Moves. J. Bridge Eng. 2019, 24, 04019002. [Google Scholar] [CrossRef] [Scilit]
  70. Bounds, W.; Tann, B. Analysis of SPMT Transport of Large Onshore Modules. In Structures Congress 2022; ASCE: Reston, VA, USA, 2022. [Google Scholar] [CrossRef] [Scilit]
  71. She, Y.X. The Force Analysis of Landing Stage and Transportation Terminal of Large Module with SPMT Trolley. Appl. Mech. Mater. 2013, 467, 349–353. [Google Scholar] [CrossRef] [Scilit]
  72. International Maritime Organisation. IMO/ILO/UNECE Code of Practice for Packing of Cargo Transport Units; Maritime Safety Committee: London, UK, 2014. [Google Scholar]
  73. DNV. Route-Specific Cargo Calculator. 2025. Available online: https://www.dnv.com/services/route-specific-cargo-calculator/ (accessed on 9 September 2025).
  74. Liu, Z.; Hai, X.; Ji, A.; Liang, C.; Cheng, Y. Module and Vessel Interaction Analysis for Module Ocean Transportation. In Proceedings of the ASME 2013 32nd International Conference on Ocean, Offshore and Arctic Engineering; Volume 1: Offshore Technology; ASME: New York, NY, USA, 2013. [Google Scholar] [CrossRef] [Scilit]
  75. Ma, Y.; Chen, G. Calculation and Analysis of Sea-Fastening Support and Welding Strength of Topside Module. J. Phys. Conf. Ser. 2022, 2174, 12067. [Google Scholar] [CrossRef] [Scilit]
  76. Soules, J.G. Truck Transport and Lifting Design Criteria for Onshore Modular Pre-Assembled Units. In Structures Congress 2020; ASCE: Reston, VA, USA, 2020; pp. 599–612. [Google Scholar] [CrossRef] [Scilit]
  77. National Transport Commission. Load Restraint Guide: Guidelines and Performance Standards for the Safe Carriage of Loads on Road Vehicles; National Transport Commission: Melbourne, Australia, 2004.
  78. Szabo, R. Collapse Damages Mine Equipment, Injures Worker. Australasian Mine Safety Journal. 15 June 2022. Available online: https://www.amsj.com.au/collapse-damages-mine-equipment-injures-worker/ (accessed on 8 September 2024).
  79. Government of Western Australia. Mine Safety Bulletin No 124; Government of Western Australia: Perth, Australia, 2015.
  80. Lam, M.; Ahmed, E. Experimental Database for Steel Flush End-Plate Connections. J. Struct. Eng. 2021, 147, 04721006. [Google Scholar] [CrossRef] [Scilit]
  81. Shrih, A.; Rahman, A.; Al-Jabri, K.S. Finite Element Analyses of Flush End-Plate Connections between Steel Beams and Columns at Elevated Temperatures. Adv. Struct. Eng. 2009, 12, 311–324. [Google Scholar] [CrossRef] [Scilit]
  82. Elkady, A. Response Characteristics of Flush End-Plate Connections. Eng. Struct. 2022, 269, 114856. [Google Scholar] [CrossRef] [Scilit]
  83. Liu, X.; Hao, Z. Constitutive Model for Rotation Behaviour of Semi-Rigid Steel Beam-to-Column Joints. J. Constr. Steel Res. 2022, 198, 107563. [Google Scholar] [CrossRef] [Scilit]
  84. AS 4100:2020; Steel Structures. SAI Global Limited: Sydney, Australia, 2020.
  85. Higgs, C. The Position and Verticality of Structural Steel. In Proceedings of the 20th Association of Public Authority Surveyors Conference (APAS2015), Coffs Harbour, Australia, 16–18 March 2015; Available online: https://www.apas.org.au/files/conferences/2015/The-Position-and-Verticality-of-Structural-Steel.pdf (accessed on 3 December 2024).
  86. Tzimas, A.S.; Skalomenos, K.A.; Beskos, D.E.; Tzimas, A.S.; Skalomenos, K.A.; Beskos, D.E. A Hybrid Seismic Design Method for Steel Irregular Space Moment Resisting Frames. J. Earthq. Eng. JEE 2022, 26, 1657–1692. [Google Scholar] [CrossRef] [Scilit]
  87. Aninthaneni, P.K.; Dhakal, R.P.; Aninthaneni, P.K.; Dhakal, R.P. Prediction of Fundamental Period of Regular Frame Buildings. Bull. New Zealand Soc. Earthq. Eng. 2016, 49, 175–189. [Google Scholar] [CrossRef] [Scilit]
  88. Sadashiva, V.K.; Macrae, G.A.; Deam, B.L.; Sadashiva, V.K.; Macrae, G.A.; Deam, B.L. Determination of Structural Irregularity Limits. Bull. New Zealand Soc. Earthq. Eng. 2009, 42, 288–301. [Google Scholar] [CrossRef] [Scilit]
  89. AS 2670.1:2001; Evaluation of Human Exposure to Whole-Body Vibration Part: General Requirements. SAI Global Limited: Sydney, Australia, 2001.
  90. AS ISO 2631.2:2014; Mechanical Vibration and Shock—Evaluation of Human Exposure to Whole-Body Vibration Part2: Vibration in Buildings (1 Hz to 80 Hz). SAI Global Limited: Sydney, Australia, 2014.
  91. Australian Government. Work Health and Safety Act 2011; Australian Government: Canberra, Australia, 2018.
  92. Queensland Government. Steel Construction—Code of Practice 2004; Relations WHaSQ-OoI, Ed.; Queensland Government: Brisbane, Australia, 2018.
  93. Government of Western Australia. Lifting, Lowering or Suspending Loads; Department of Energy M, Industry Regulation and Safety, Eds.; Government of Western Australia: Perth, Australia, 2022.
  94. Government of Western Australia. Safe Work Method Statement for High Risk Construction Work; Department of Energy M, Industry Regulation and Safety, Eds.; Government of Western Australia: Perth, Australia, 2022. [Google Scholar]
  95. Government of Western Australia. Code of Practice—Construction Work; Department of Energy M, Industry Regulation and Safety, Eds.; Government of Western Australia: Perth, Australia, 2022.
  96. WorkSafe Victoria. Safe Erection of Structural Steel for Buildings; Victorian WorkCover Authority: Melbourne, Australia, 2009.
  97. The British Constructional Steelwork Association Ltd. BCSA Code of Practice for Erection of Multi-Storey Buildings; The British Constructional Steelwork Association Ltd.: London, UK, 2006. [Google Scholar]
  98. AS/NZS 5131:2016; Structural Steelwork—Fabrication and Erection. SAI Global Limited: Sydney, Australia, 2016.
  99. Saurabh, A.; Shah, M.B.K. Guidelines for Erection process of Pre-Engineered Building. Int. J. Eng. Tech. Res. (IJETR) 2015, 3, 2321-0869. [Google Scholar]
  100. Viana, D.D.; Tommelein, I.D.; Formoso, C.T. Using Modularity to Reduce Complexity of Industrialized Building Systems for Mass Customization. Energies 2017, 10, 1622. [Google Scholar] [CrossRef] [Scilit]
  101. Boulos, T.; Meney, D.; Vimonsatit, V. Steel Friction only Connections for Modular Construction (Part 1). In Proceedings of the Australian Structural Engineering Conference: ASEC 2018, Adelaide, Australia, 25–28 September 2018. [Google Scholar]
  102. Liu, X.; Zhou, X.; Zhang, A.; Tian, C.; Zhang, X.; Tan, Y. Design and Compilation of Specifications for a Modular-Prefabricated High-Rise Steel Frame Structure with Diagonal Braces. Part I: Integral Structural Design. Struct. Des. Tall Spec. Build. 2018, 27, e1415. [Google Scholar] [CrossRef] [Scilit]
  103. Vincent, V.; William, M.; Lu, L.-W. Automated Construction in the Atlss Integrated Building Systems. Autom. Constr. 1994, 3, 35–43. [Google Scholar] [CrossRef] [Scilit]
  104. Colville, J.M.; Amde, A. Research Transformed into Practice: Implementation of Nsf Research. 1995. Available online: https://ebookcentral.proquest.com/lib/curtin/detail.action?docID=3115422 (accessed on 12 April 2025).
  105. Renz, B. Innovative Connections. Modern Steel Construction; AISC: Chicago, IL, USA, 2005; Available online: https://www.aisc.org/globalassets/modern-steel/archives/2005/08/2005v08_innovative_connections.pdf (accessed on 1 October 2025).
  106. Schultz, A.E.; Le, J.-L.; Shemshadian, M.E.; Labbane, R.; Laefer, D.F.; Al-Sabah, S.; Truong-Hong, L.; Huyn, M.; Mcgetrick, P.; Martin, T.; et al. Advanced Manufacturing for the Assembly of Structural Steel. Interdependence between Structural Engineering and Construction Management. Pract. Period. Struct. Des. Constr. 2021, 26, 04020052. [Google Scholar] [CrossRef] [Scilit]
  107. Labbane, R. Experimental Investigation of the Performance of Intermeshed Steel Beam Connections; University Digital Conservancy: Minneapolis, MN, USA, 2019; Available online: https://hdl.handle.net/11299/206158 (accessed on 9 October 2025).
  108. Wang, H.; Zhang, B.; Qian, H.; Liu, J.; An, B.; Fan, F. Experimental and Numerical Studies of a New Prefabricated Steel Frame Joint Without Field-Welding: Design and Static Performance. Thin-Walled Struct. 2021, 159, 107271. [Google Scholar] [CrossRef] [Scilit]
  109. Yang, N.; Xia, J.; Chang, H.; Zhang, L.; Yang, H. A Novel Plug-in Self-Locking Inter-Module Connection for Modular Steel Buildings. Thin-Walled Struct. 2023, 187, 110774. [Google Scholar] [CrossRef] [Scilit]
  110. Lee, S.S.; Park, K.S.; Jung, J.S.; Lee, K.S. Evaluation of the Structural Performance of a Novel Methodology for Connecting Modular Units Using Straight and Cross-Shaped Connector Plates in Modular Buildings. Appl. Sci. 2020, 10, 8186. [Google Scholar] [CrossRef] [Scilit]
  111. Khan, K.; Chen, Z.H.; Liu, J.D.; Yan, J.B. Simplified Modelling of Novel Non-Welded Joints for Modular Steel Buildings. Adv. Steel Constr. 2021, 17, 412–424. [Google Scholar] [CrossRef] [Scilit]
  112. Dai, Z.; Cheong, T.Y.C.; Pang, S.D.; Liew, J.Y.R. Experimental Study of Grouted Sleeve Connections under Bending for Steel Modular Buildings. Eng. Struct. 2021, 243, 1. [Google Scholar] [CrossRef] [Scilit]
  113. Shi, F.W.; Li, Y.M. Innovative Inner Sleeve Composite Bolted Connections for Modular Steel Constructions: Experimental and Numerical Studies. J. Build. Eng. 2023, 64, 105624. [Google Scholar] [CrossRef] [Scilit]
  114. Shi, F.W.; Ding, Y.; Zong, L.; Meng, X.; Chen, Y. Axial Mechanical Behavior of Innovative Inter-Module Connection for Modular Steel Constructions. J. Build. Eng. 2023, 65, 105765. [Google Scholar] [CrossRef] [Scilit]
  115. Liu, Z.; Wang, Y.; Zhang, Z.; Wu, W. Experimental Study on Seismic Cyclic Behavior of an Innovative Blind Bolted Connection Joint Between Modules in Modular Steel Frame. Structures 2023, 52, 158–174. [Google Scholar] [CrossRef] [Scilit]
  116. Liu, J.; Chen, Z.; Liu, Y.; Bai, Y.; Zhong, X. Full-Scale Corner-Supported Modular Steel Structures with Vertical Inter-Module Connections Under Cyclic Loading. J. Build. Eng. 2021, 44, 103269. [Google Scholar] [CrossRef] [Scilit]
  117. Corfar, D.A.; Tsavdaridis, K.D. A Comprehensive Review and Classification of Inter-Module Connections for Hot-Rolled Steel Modular Building Systems. J. Build. Eng. 2022, 50, 104006. [Google Scholar] [CrossRef] [Scilit]
  118. Chen, Z.; Wang, J.; Liu, J.; Cong, Z. Tensile and Shear Performance of Rotary Inter-Module Connection for Modular Steel Buildings. J. Constr. Steel Res. 2020, 175, 106367. [Google Scholar] [CrossRef] [Scilit]
  119. Chen, Z.; Liu, J.; Yu, Y.; Zhou, C.; Yan, R. Experimental Study of an Innovative Modular Steel Building Connection. J. Constr. Steel Res. 2017, 139, 69–82. [Google Scholar] [CrossRef] [Scilit]
  120. Chen, Z.; Liu, J.; Yu, Y. Experimental Study on Interior Connections in Modular Steel Buildings. Eng. Struct. 2017, 147, 625–638. [Google Scholar] [CrossRef] [Scilit]
  121. Chen, H.L.; Ke, C.; Chen, C.; Li, G.Q. Study on the Shear Behavior of Inter-Module Connection with a Bolt and Shear Key Fitting for Modular Steel Buildings. Adv. Struct. Eng. 2023, 26, 218–233. [Google Scholar] [CrossRef] [Scilit]
  122. Chen, H.L.; Cao, K.; Chen, C.; Li, G.Q. Research on the Flexural Behavior of a Novel Inter-Module Connection with a Bolt and Shear Key Fitting for Modular Steel Buildings. Adv. Struct. Eng. 2023, 26, 640–657. [Google Scholar] [CrossRef] [Scilit]
  123. Lacey, A.W.; Chen, W.; Hao, H.; Bi, K. New Interlocking Inter-Module Connection for Modular Steel Buildings: Experimental and Numerical Studies. Eng. Struct. 2019, 198, 109465. [Google Scholar] [CrossRef] [Scilit]
  124. Lacey, A.W.; Chen, W.; Hao, H.; Bi, K. New Interlocking Inter-Module Connection for Modular Steel Buildings: Simplified Structural Behaviours. Eng. Struct. 2021, 227, 111409. [Google Scholar] [CrossRef] [Scilit]
  125. Liu, X.C.; Zhan, X.X.; Pu, S.H.; Zhang, A.L.; Xu, L. Seismic performance study on slipping bolted truss-to-column connections in modularized prefabricated steel structures. Eng. Struct. 2018, 163, 241–254. [Google Scholar] [CrossRef] [Scilit]
  126. Liu, X.C.; Pu, S.H.; Zhang, A.L.; Zhan, X.X. Performance analysis and design of bolted connections in modularized prefabricated steel structures. J. Constr. Steel Res. 2017, 133, 360–373. [Google Scholar] [CrossRef] [Scilit]
  127. Liu, X.C.; Yang, Z.W.; Wang, H.X.; Zhang, A.L.; Pu, S.H.; Chai, S.T.; Wu, L. Seismic performance of H-section beam to HSS column connection in prefabricated structures. J. Constr. Steel Res. 2017, 138, 1–16. [Google Scholar] [CrossRef] [Scilit]
  128. Chen, Z.; Niu, X.; Liu, J.; Khan, K.; Liu, Y. Seismic Study on an Innovative Fully-Bolted Beam-Column Joint in Prefabricated Modular Steel Buildings. Eng. Struct. 2021, 234, 111875. [Google Scholar] [CrossRef] [Scilit]
  129. Chen, S.; Teng, X.; Sang, X.; Ye, B.; Liang, Z. Study on Geometric Optimization for New Type of Steel Mortise and Tenon Joint Based on Performance. IOP Conf. Ser. Earth Environ. Sci. 2021, 676, 12039. [Google Scholar] [CrossRef] [Scilit]
  130. Twizere, M.; Taşkın, K. Development of a Novel I-Beam to Box Column Connection with Welded Steel Plates. Struct. Des. Tall Spec. Build. 2022, 31, e1940. [Google Scholar] [CrossRef] [Scilit]
  131. Shaheen, M.A. A New Idea to Improve the Cyclic Performance of End Plate Beam–Column Connections. Eng. Struct. 2022, 253, 113759. [Google Scholar] [CrossRef] [Scilit]
  132. Li, Z.; Qi, Y.; Teng, J. Experimental Investigation of Prefabricated Beam-to-Column Steel Joints for Precast Concrete Structures Under Cyclic Loading. Eng. Struct. 2020, 209, 110217. [Google Scholar] [CrossRef] [Scilit]
  133. Bishay-Girges, N.W. Improved Steel Beam-Column Connections in Industrial Structures. Eng. Technol. Appl. Sci. Res. 2020, 10, 5126–5131. [Google Scholar] [CrossRef] [Scilit]
  134. Yang, H. Performance analysis of Semi-Rigid Connections in Prefabricated High-Rise Steel Structures. Structures 2020, 28, 837–846. [Google Scholar] [CrossRef] [Scilit]
  135. Iyama, J.; Fukushima, Y.; Araki, K.; Piao, S.; Hirosawa, K.; Sato, N.; Ohata, E. Cyclic Behavior of a New Mechanical Beam-to-Column Connection for Steel Structures. In Proceedings of the Conference on Behaviour of Steel Structures in Seismic Areas, Santiago, Chile, 9–11 January 2012; CRC Press: Boca Raton, FL, USA, 2012; pp. 179–185. [Google Scholar] [CrossRef] [Scilit]
  136. Al Sabah, S.A.; Laefer, D.F. Structural Member. UK Patent Application No. 1718744.4, 13 November 2017. [Google Scholar]
  137. Al Sabah, S.A.; Laefer, D.F. Structural Member. UK Patent Application No. 1718746.9, 13 November 2017. [Google Scholar]
  138. ANSI/AISC 360-22; Specification for Structural Steel Buildings. ANSI/AISC: Chicago, IL, USA, 2005.
  139. EN 1993-1-1:2005; Design of Steel Structures—Part 1-1: General Rules and Rules for Buildings. European Committee for Standardization (CEN): Brussels, Belgium, 2005.
  140. Shemshadian, M.E.; Schultz, A.E.; Le, J.-L.; Laefer, D.F.; Al-Sabah, S.; Mcgetrick, P. Structural Mechanics Characterization of Steel Intermeshed Connection Using Nonlinear Finite Element Analysis. Eng. Struct. 2021, 238, 112264. [Google Scholar] [CrossRef] [Scilit]
  141. Shemshadian, M.E. Structural Mechanics Characterization of Steel Intermeshed Connections. 2020. Available online: https://hdl.handle.net/11299/216340 (accessed on 7 February 2025).
  142. Yu, D.; Kong, I.; Lu, M. Applying Ancient Structural Principles to a New Prefabricated Steel System. CTBUH J. 2018, 1, 36–43. Available online: https://www.jstor.org/stable/90021074 (accessed on 4 February 2025).
  143. Al-Sabah, S.; Laefer, D.F.; Truong Hong, L.; Phuoc Huynh, M.; Le, J.-L.; Martin, T.; Matis, P.; McGetrick, P.; Schultz, A.; Shemshadian, M.E.; et al. Introduction of the Intermeshed Steel Connection—A New Universal Steel Connection. Buildings 2020, 10, 37. [Google Scholar] [CrossRef] [Scilit]
  144. Thongchom, C.; Ghamari, A.; Karimi, I. Improving the Cyclic Behavior and Post-Fire Performance of the Prequalified ConXL Connection. Struct. Des. Tall Spec. Build. 2025, 34, e70023. [Google Scholar] [CrossRef] [Scilit]
  145. Symmons, R.; ConXtech Inc. Patent Issued for Box Column Assembly (USPTO 9815151). U.S. Patent 9,815,151 B2, 14 November 2017. [Google Scholar]
  146. ANSI/AISC 358-22; Prequalified Connections for Special and Intermediate Steel Moment Frames for Seismic Applications. American Institute of Steel Construction: Chicago, IL, USA, 2022.
  147. ANSI/AISC 358-16; Prequalified Connections for Special and Intermediate Steel Moment Frames for Seismic Applications. American Institute of Steel Construction: Chicago, IL, USA, 2016.
  148. ANSI/AISC 341-16; Seismic Provisions for Strucutral Steel Buildings. American Institute of Steel Construction: Chicago, IL, USA, 2016.
  149. Gao, Z.; Meney, D.; Vimosatit, V. Steel Friction only Connections for Modular Construction (Part 2). In Proceedings of the Australian Structural Engineering Conference: ASEC 2018, Adelaide, Australia, 25–28 September 2018. [Google Scholar]
  150. Westdorp, B.; Meney, D. AltCONNECT®—An Innovative Structural Steel Connection Without Bolts or Welds. In Proceedings of the Australian Structural Engineering Conference 2020, Online, 11–13 November 2020; Available online: https://microsites.arinex.com.au/asec2020/pdf/full-paper_71.pdf (accessed on 7 January 2024).
  151. Garlock, R.B.; Viscomi, B.V.; Lu, L.-W. ATLSS Connections with Moment Capacity. Ph.D. Thesis, Lehigh University, Bethlehem, PA, USA, 1993. [Google Scholar]
  152. Lawrence, W.S.L.; Viscomi, V.B.L. Advanced connections reduce cost. In Modern Steel Construction; American Institute of Steel Construction: Chicago, IL, USA, 1993; pp. 16–21. [Google Scholar]
  153. Ghassemieh, M.; Sokhtesaraei, M.H.; Akbarpour, H. Development of a New Cyclic Loading Protocol for Seismic Performance Assessment of Steel Moment Connections. J. Earthq. Eng. 2022, 26, 8305–8331. [Google Scholar] [CrossRef] [Scilit]
  154. Applied Technology Council. Guidelines for Cyclic Seismic Testing of Components of Steel Structures; ATC-24; Applied Technology Council: Redwood City, CA, USA, 1992. [Google Scholar]
  155. Clark, P. Protocol for Fabrication, Inspection, Testing and Documentation of Beam-Column Connection Tests and Other Experimental Specimens; SAC Joint Venture; APTECO: Sydney, Australia, 1997. [Google Scholar]
Figure 1. Typical process mining structure. Photograph courtesy of Process 26 Pty Ltd., Perth, Western Australia. Used with permission.
Buildings 16 01675 g001
Figure 2. (a) Gravity loads due to ore spillage. Photograph courtesy of Process 26 Pty Ltd. Used with permission. (b) Ore spillage on the walkway. Reproduced from AT Mineral Processing (2024), with permission. © Jeremy Cairns [42].
Buildings 16 01675 g002
Figure 3. (a): Run-of-mine bin layout feeding a gyratory crusher. Reproduced from Naser et al. (2011) [52]. (b) Run-of-mine bin fed by a dump truck and feeding a jaw crusher. Reproduced from AT Kis Plant Pty Ltd., New South Wales, Australia (2024) [53], with permission. © Kiss Plant Pty Ltd.
Buildings 16 01675 g003
Figure 4. Jaw crusher operation and crushing mechanism: (a) Jaw crusher showing the eccentric mechanism, which produces cyclic loads, and rock feed, which generates impact forces during crushing. Reproduced from Reed et al. (2012) [54]. This material is in the public domain. (b) Mining structure including a run-of-mine bin, feeder, rock breaker and jaw crusher. Reproduced from McLanahan Corporation, Hollidaysburg, PA, USA (2023), with permission. © McLanahan Corporation [55].
Buildings 16 01675 g004
Figure 5. (a) Rock breaker clearing feed on top of a grizzly in a ROM bin. Reproduced from Duff et al. with permission [56]. (b) Structure-mounted rock breaker used to clear ROM bin of oversize. Reproduced from Creighton Rock Drill Ltd., Mississauda, ON, Canada, with permission. © Creighton Rock Drill Ltd. [57].
Buildings 16 01675 g005
Figure 6. (a) ROM bin, live grizzly feeder and rock breaker. Reproduced from Mineral Processing Solutions (2024), with permission, © Mineral Processing Solutions [58], (b) The conveyor feeds into a bin with a vibrating feeder and loads a conveyor belt. Adapted from Szczerbakowicz et al. Licensed under CC BY 4.0 [59].
Buildings 16 01675 g006
Figure 7. (a) Double crane lift. Reproduced from Roy (2017), with permission, © American Institute of Chemical Engineers (AIChE), New York, NY, USA [68]. (b) In horizontal position for transport. Photograph taken by Author Paul J Kreppold, who holds the copyright and permits its publication.
Buildings 16 01675 g007
Figure 8. Sea transport tie-down details for a volumetric module (a) support grillage, (b) shear blocks incomplete. Photographs taken by Author Paul J Kreppold, who holds the copyright and permits its publication.
Buildings 16 01675 g008
Figure 9. Load restraint forces NTC Australia. Reproduced from National Transport Commission (2004) [77], © Commonwealth of Australia.
Buildings 16 01675 g009
Figure 10. (a) FEP arrangement and (b) deformed shape. Adapted from Elkady (2022); licensed under CC BY 4.0 [82].
Buildings 16 01675 g010
Figure 11. Deflections of the integrated hull and module structural model. Reproduced from ASME, New York, NY, USA (2013) [74], with permission. © ASME.
Buildings 16 01675 g011
Figure 12. Recent developments in connection details. (a) Front intermeshed. Reproduced from Shemshadian et al. (2020), with permission, © American Society of Civil Engineers (ASCE) [106]. (b) Side intermeshed. Reproduced from Al-Sabah et al. (2020), © The Authors, published by MDPI, Basel, Switzerland [143]. (c) Dovetail connection; redrawn based on CTBUH Journal, © Council on Tall Buildings and Urban Habitat [142]. (d) ConXtech components. Reproduced from Thongchom et al. (2025), with permission, © Wiley, Hoboken, NJ, USA [144]. (e) ConXtech assembled. Reproduced from Thongchom et al. (2025), with permission, © Wiley [144].
Buildings 16 01675 g012
Figure 13. Prefabricated beam–column steel joint, adapted from Wang et al. [108].
Buildings 16 01675 g013
Figure 14. Spigot socket system. Reproduced from Boulos et al. (2018), © Engineers Australia [101].
Buildings 16 01675 g014
Figure 15. The ATLSS connection, (a) ATLSS parts, (b) ATLSS assembled. Reproduced from Lawrence et al. (1993) [152], Modern Steel Construction. © The Authors.
Buildings 16 01675 g015
Table 1. Sea transport acceleration coefficients [72].
Significant Wave HeightSecuring Direction Longitudinal   c x Transversal   c y Vertical   Down   c z
8   m < H s 12   m Longitudinal0.300.30
Transverse0.701.00
H s > 12   m Longitudinal0.400.20
Transverse0.801.00
Table 2. Transient loads on mining structures due to typical equipment.
EquipmentTransient Load TypeLoad-Sensitive Area
CrushersCyclic—SinusoidalSupporting structure
ImpactSupporting structure
BlastBin structure
FeedersCyclic—SinusoidalConnection details
ImpactConnection details
Rock BreakersImpactConnection details
ConveyorsCyclic—SinusoidalCase-by-case assessment
ImpactAt loading points
ScreensCyclic—SinusoidalSupporting structure
Grinding MillsCyclic—SinusoidalFoundations
AgitatorsCyclic—SinusoidalConnection details
Filters/PressImpactCase-by-case assessment
Dump TruckImpactComplete structure
Dump Truck-TippingImpactImpact grizzly
Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content.