3.5.1. Determination of Design Variables and Optimization Objectives
The billet temperature, extrusion speed, and billet length were selected as design variables for a three-factor, three-level Box–Behnken experimental design [
35]. The extrusion load (which F represents), speed deviation (which VDD represents), average strain (which
represents) of the profile cross-section, and temperature difference (which
represents) of the profile cross-section were chosen as optimization objectives for multi-objective optimization. The synergistic effects of the four process parameters on the extrusion formability of the profile were investigated. The design variables and their ranges are shown in
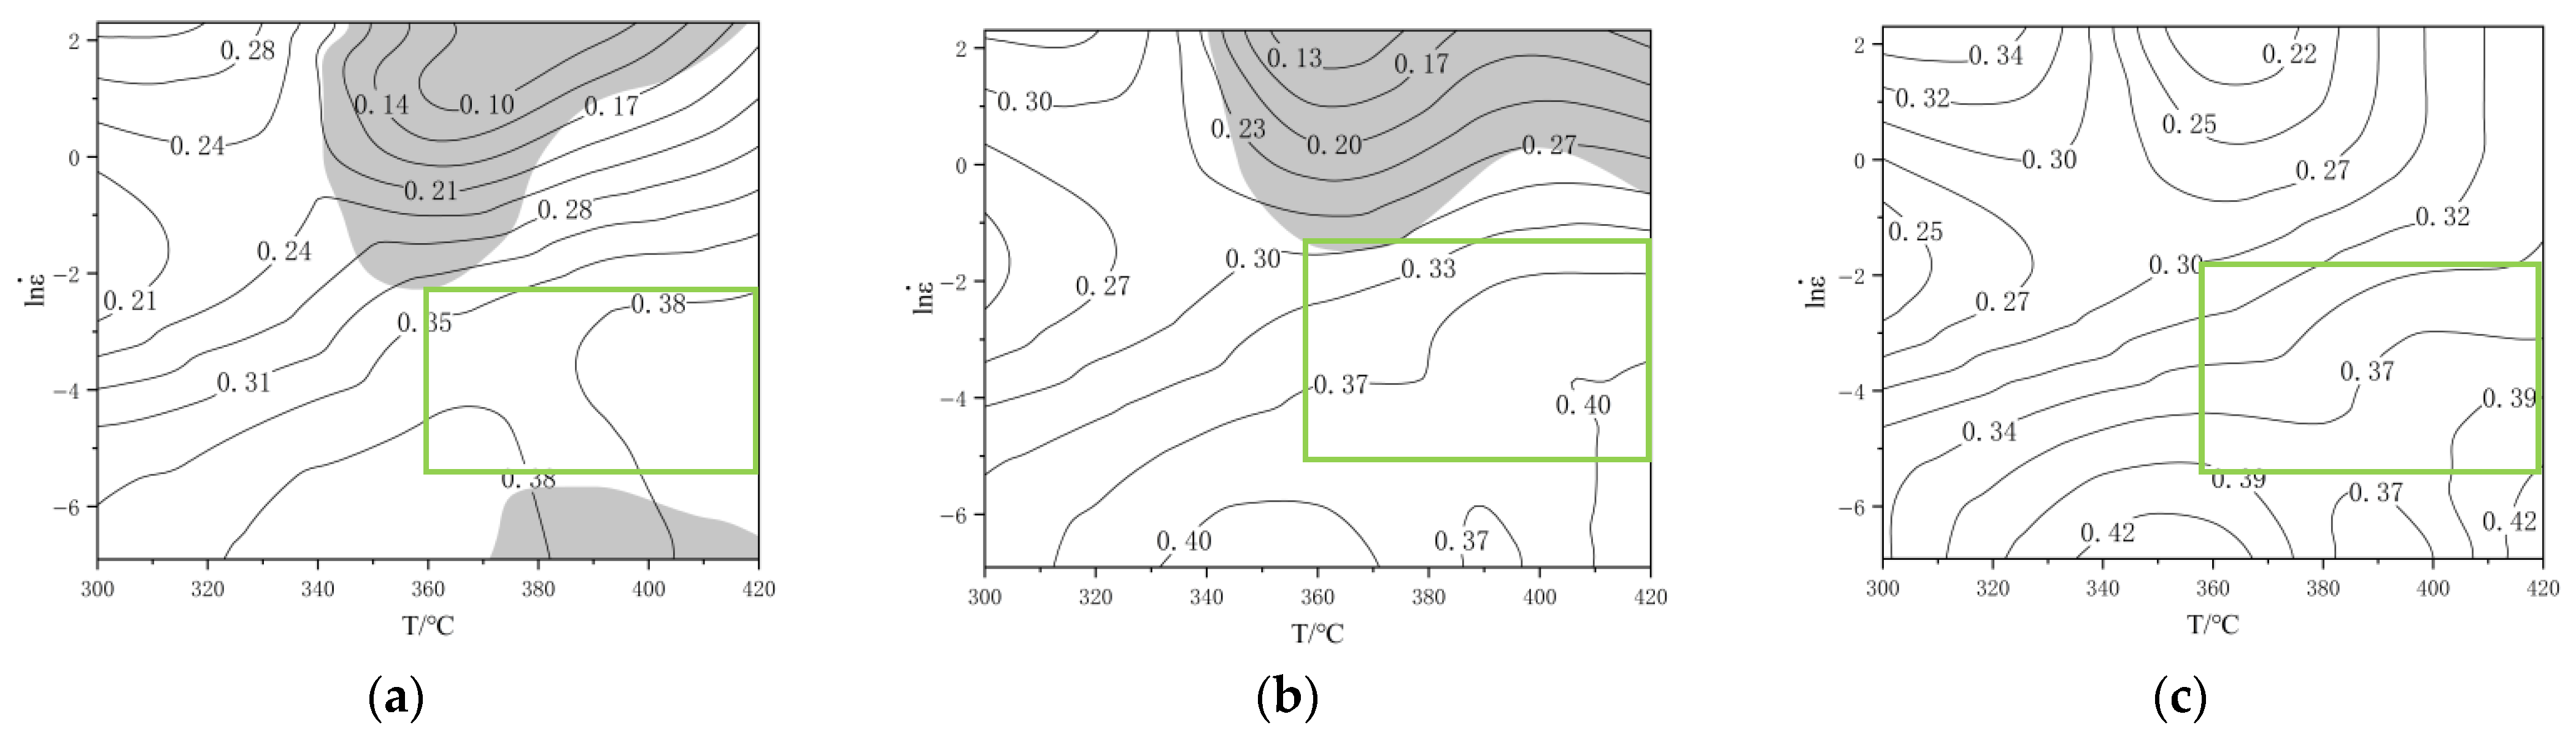
Table 5. Based on the optimal process window determined from the thermal processing diagram (
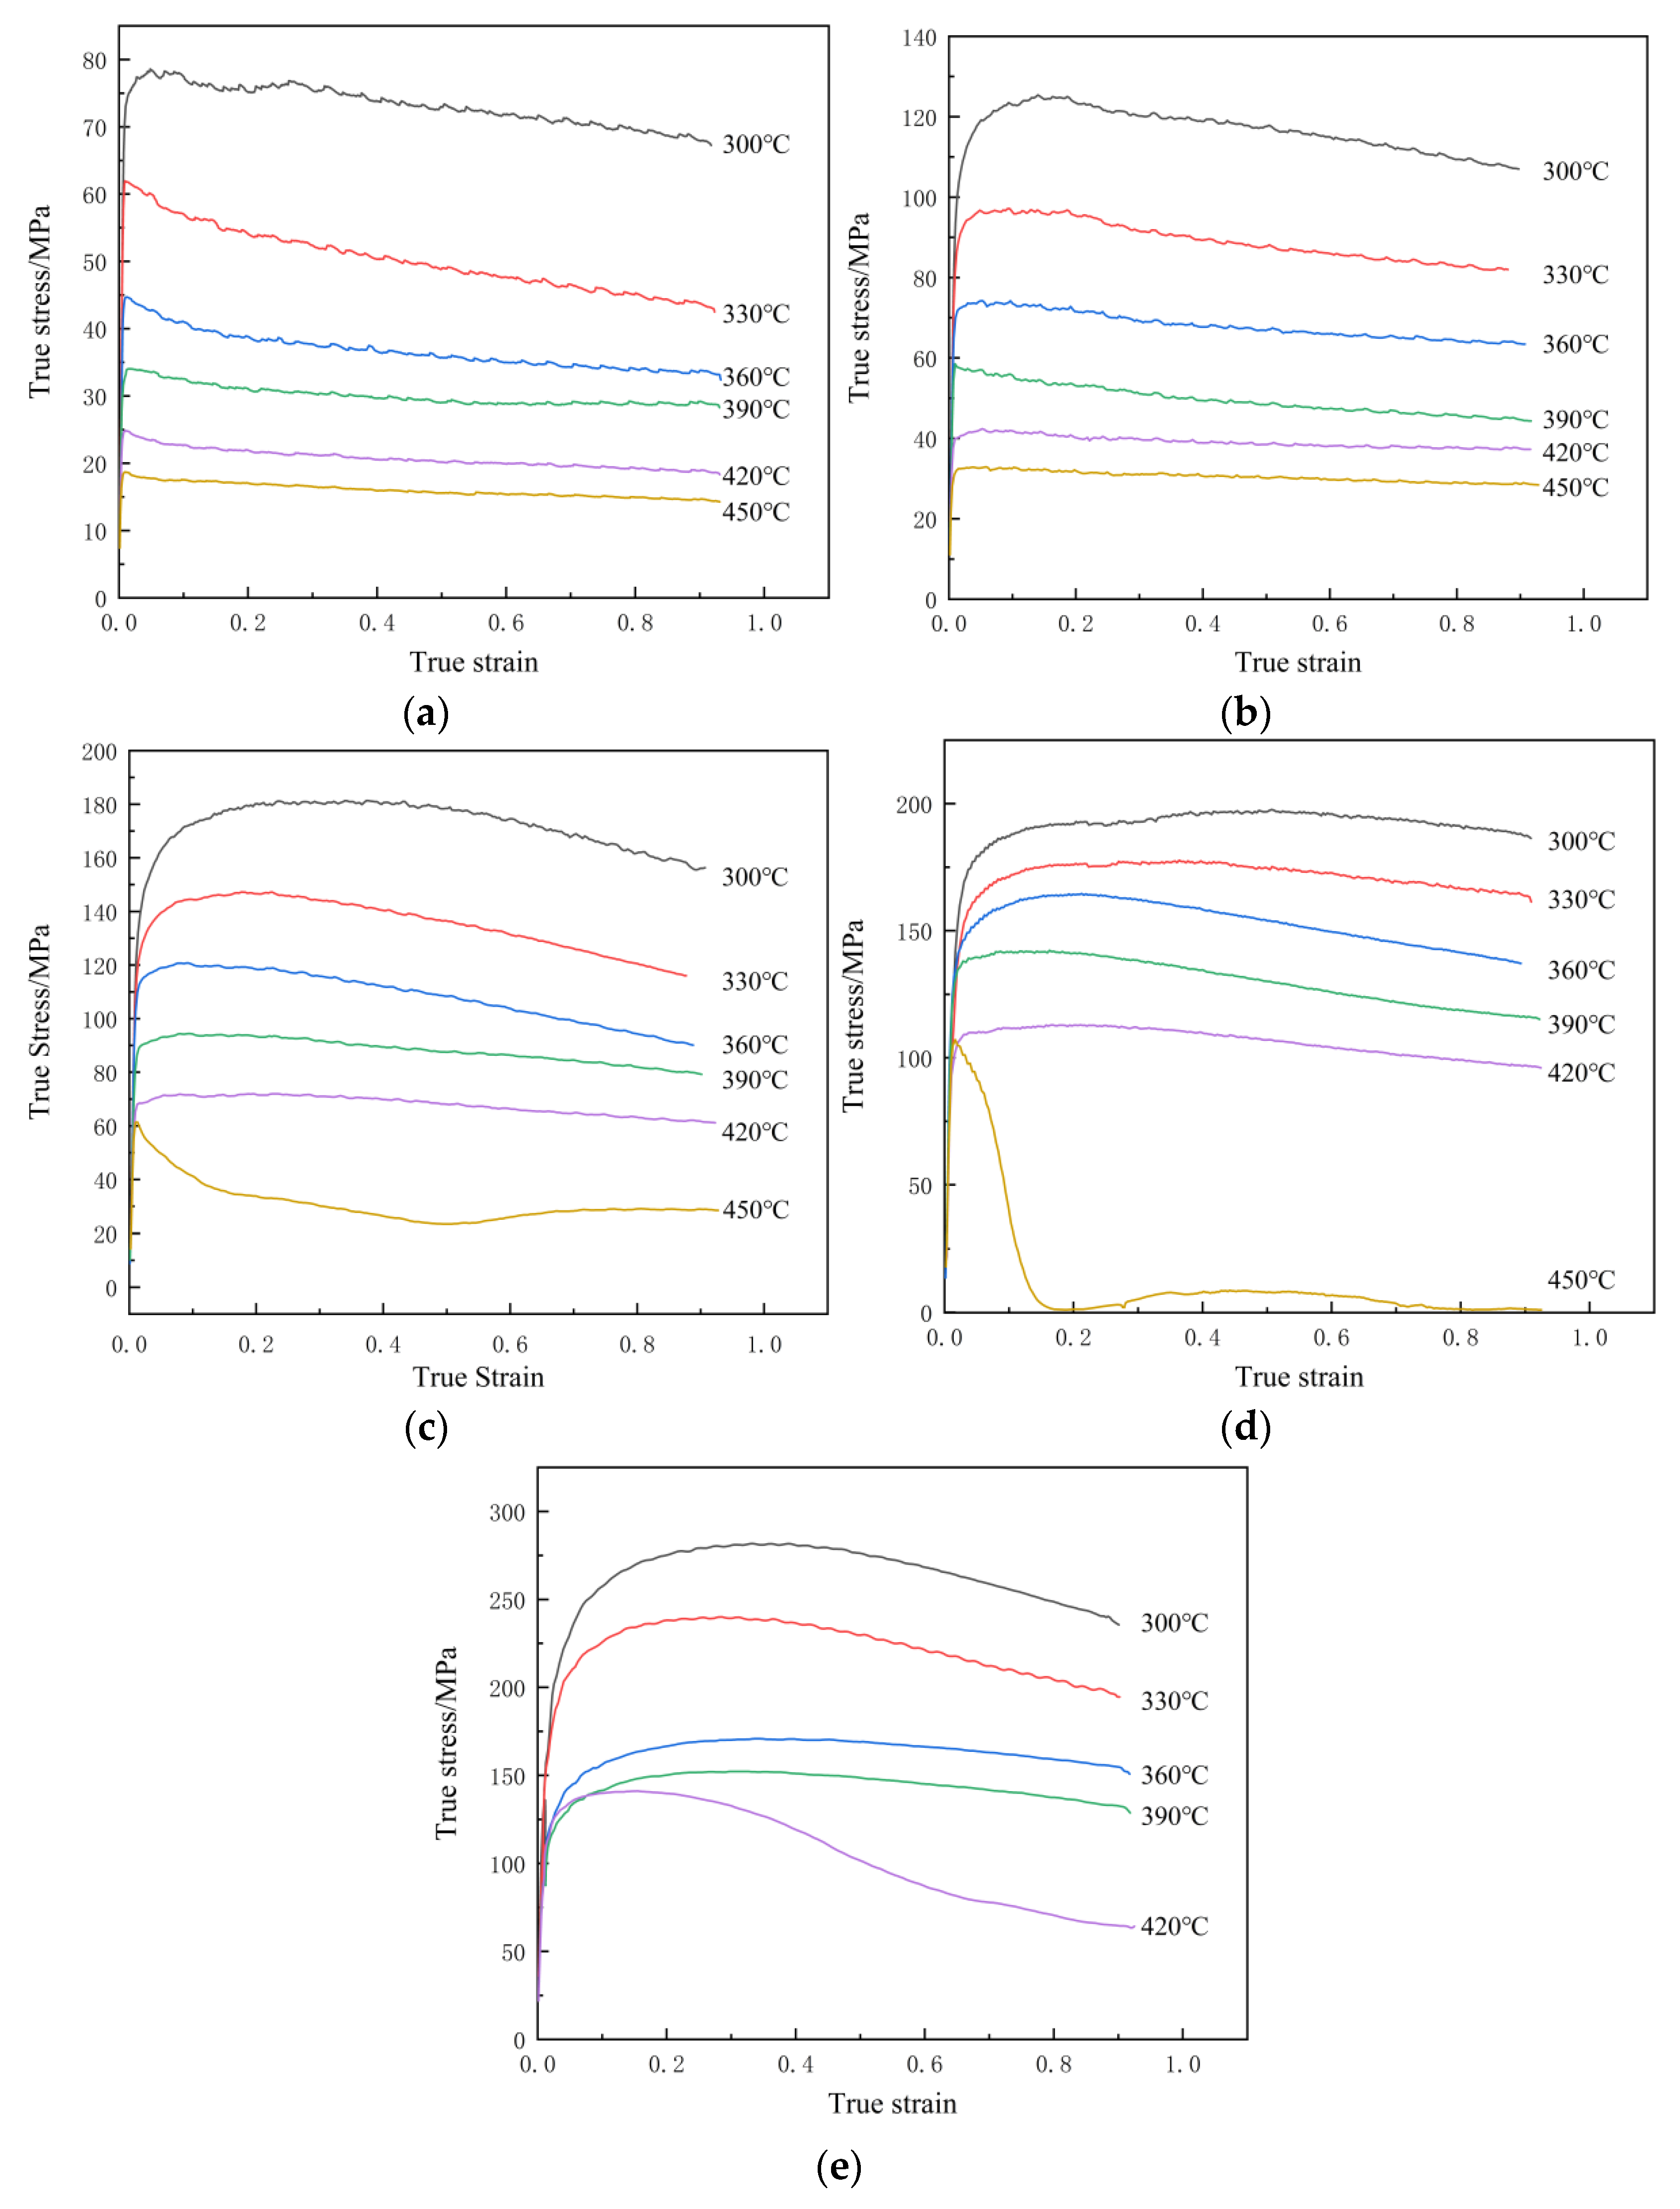
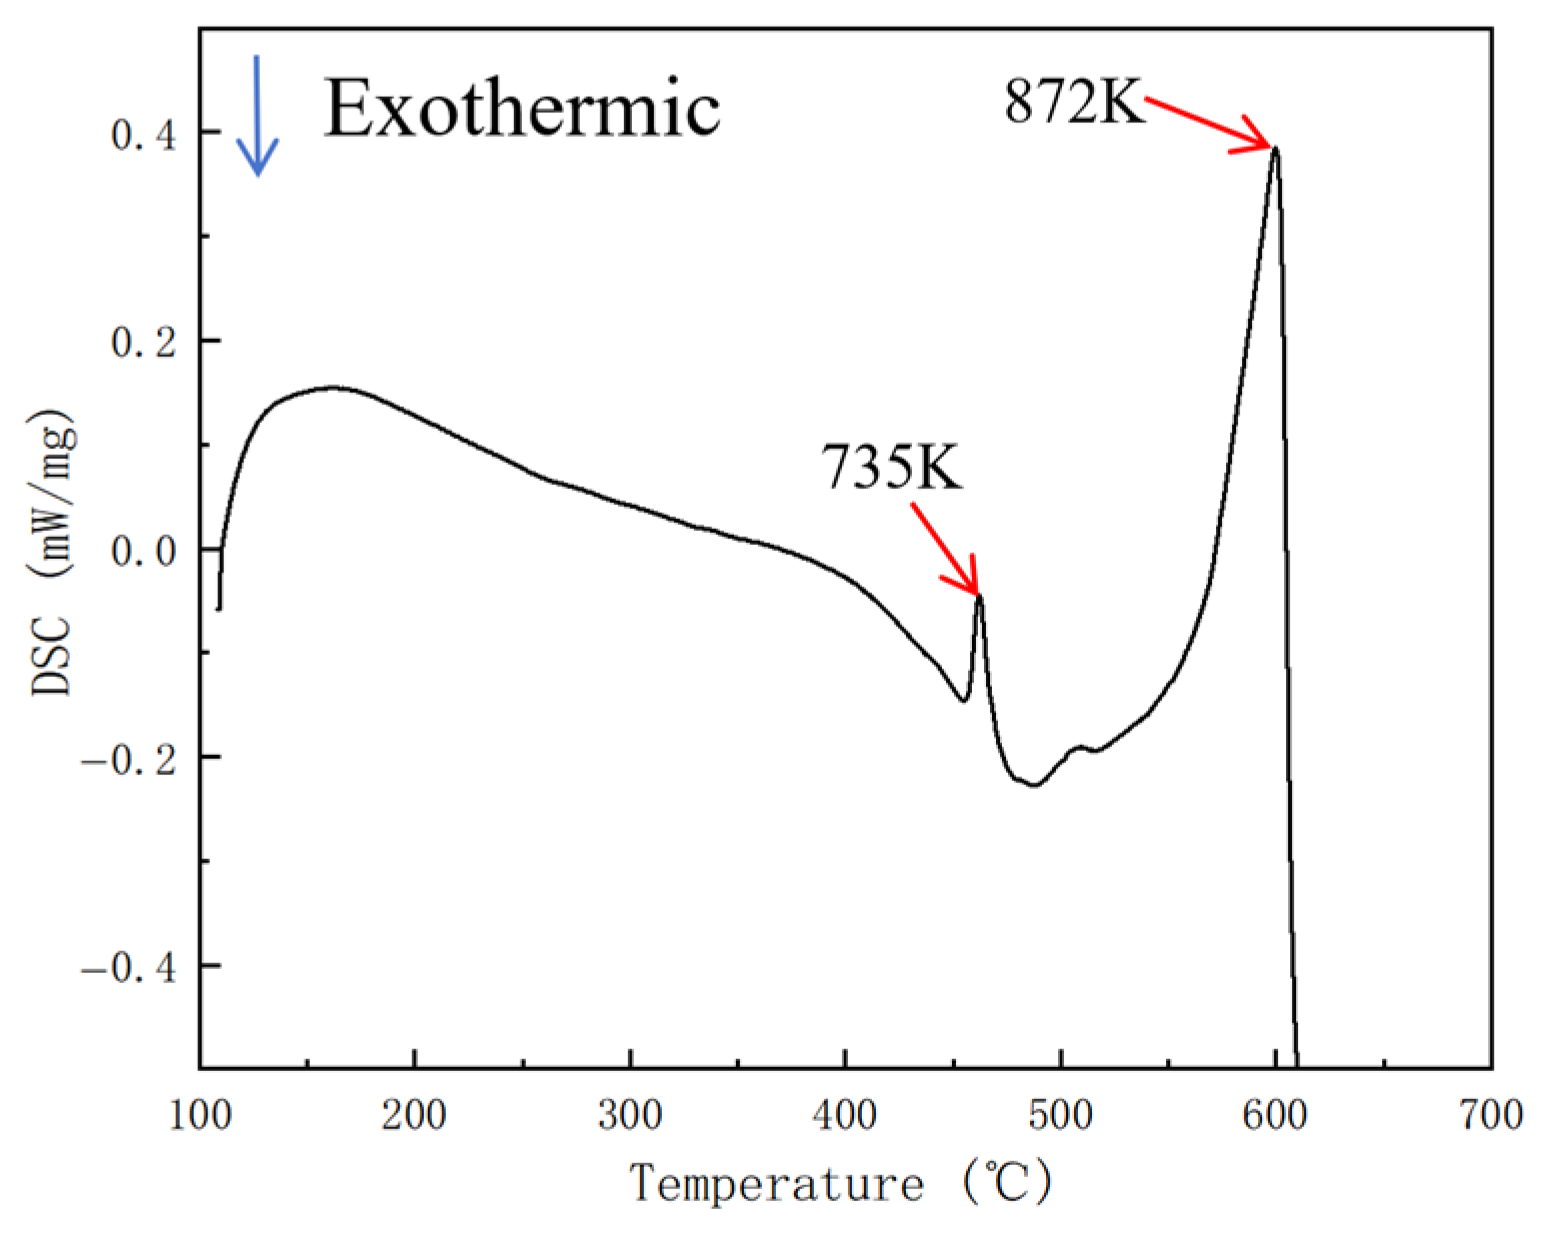
Figure 10), the three levels of the billet temperature,
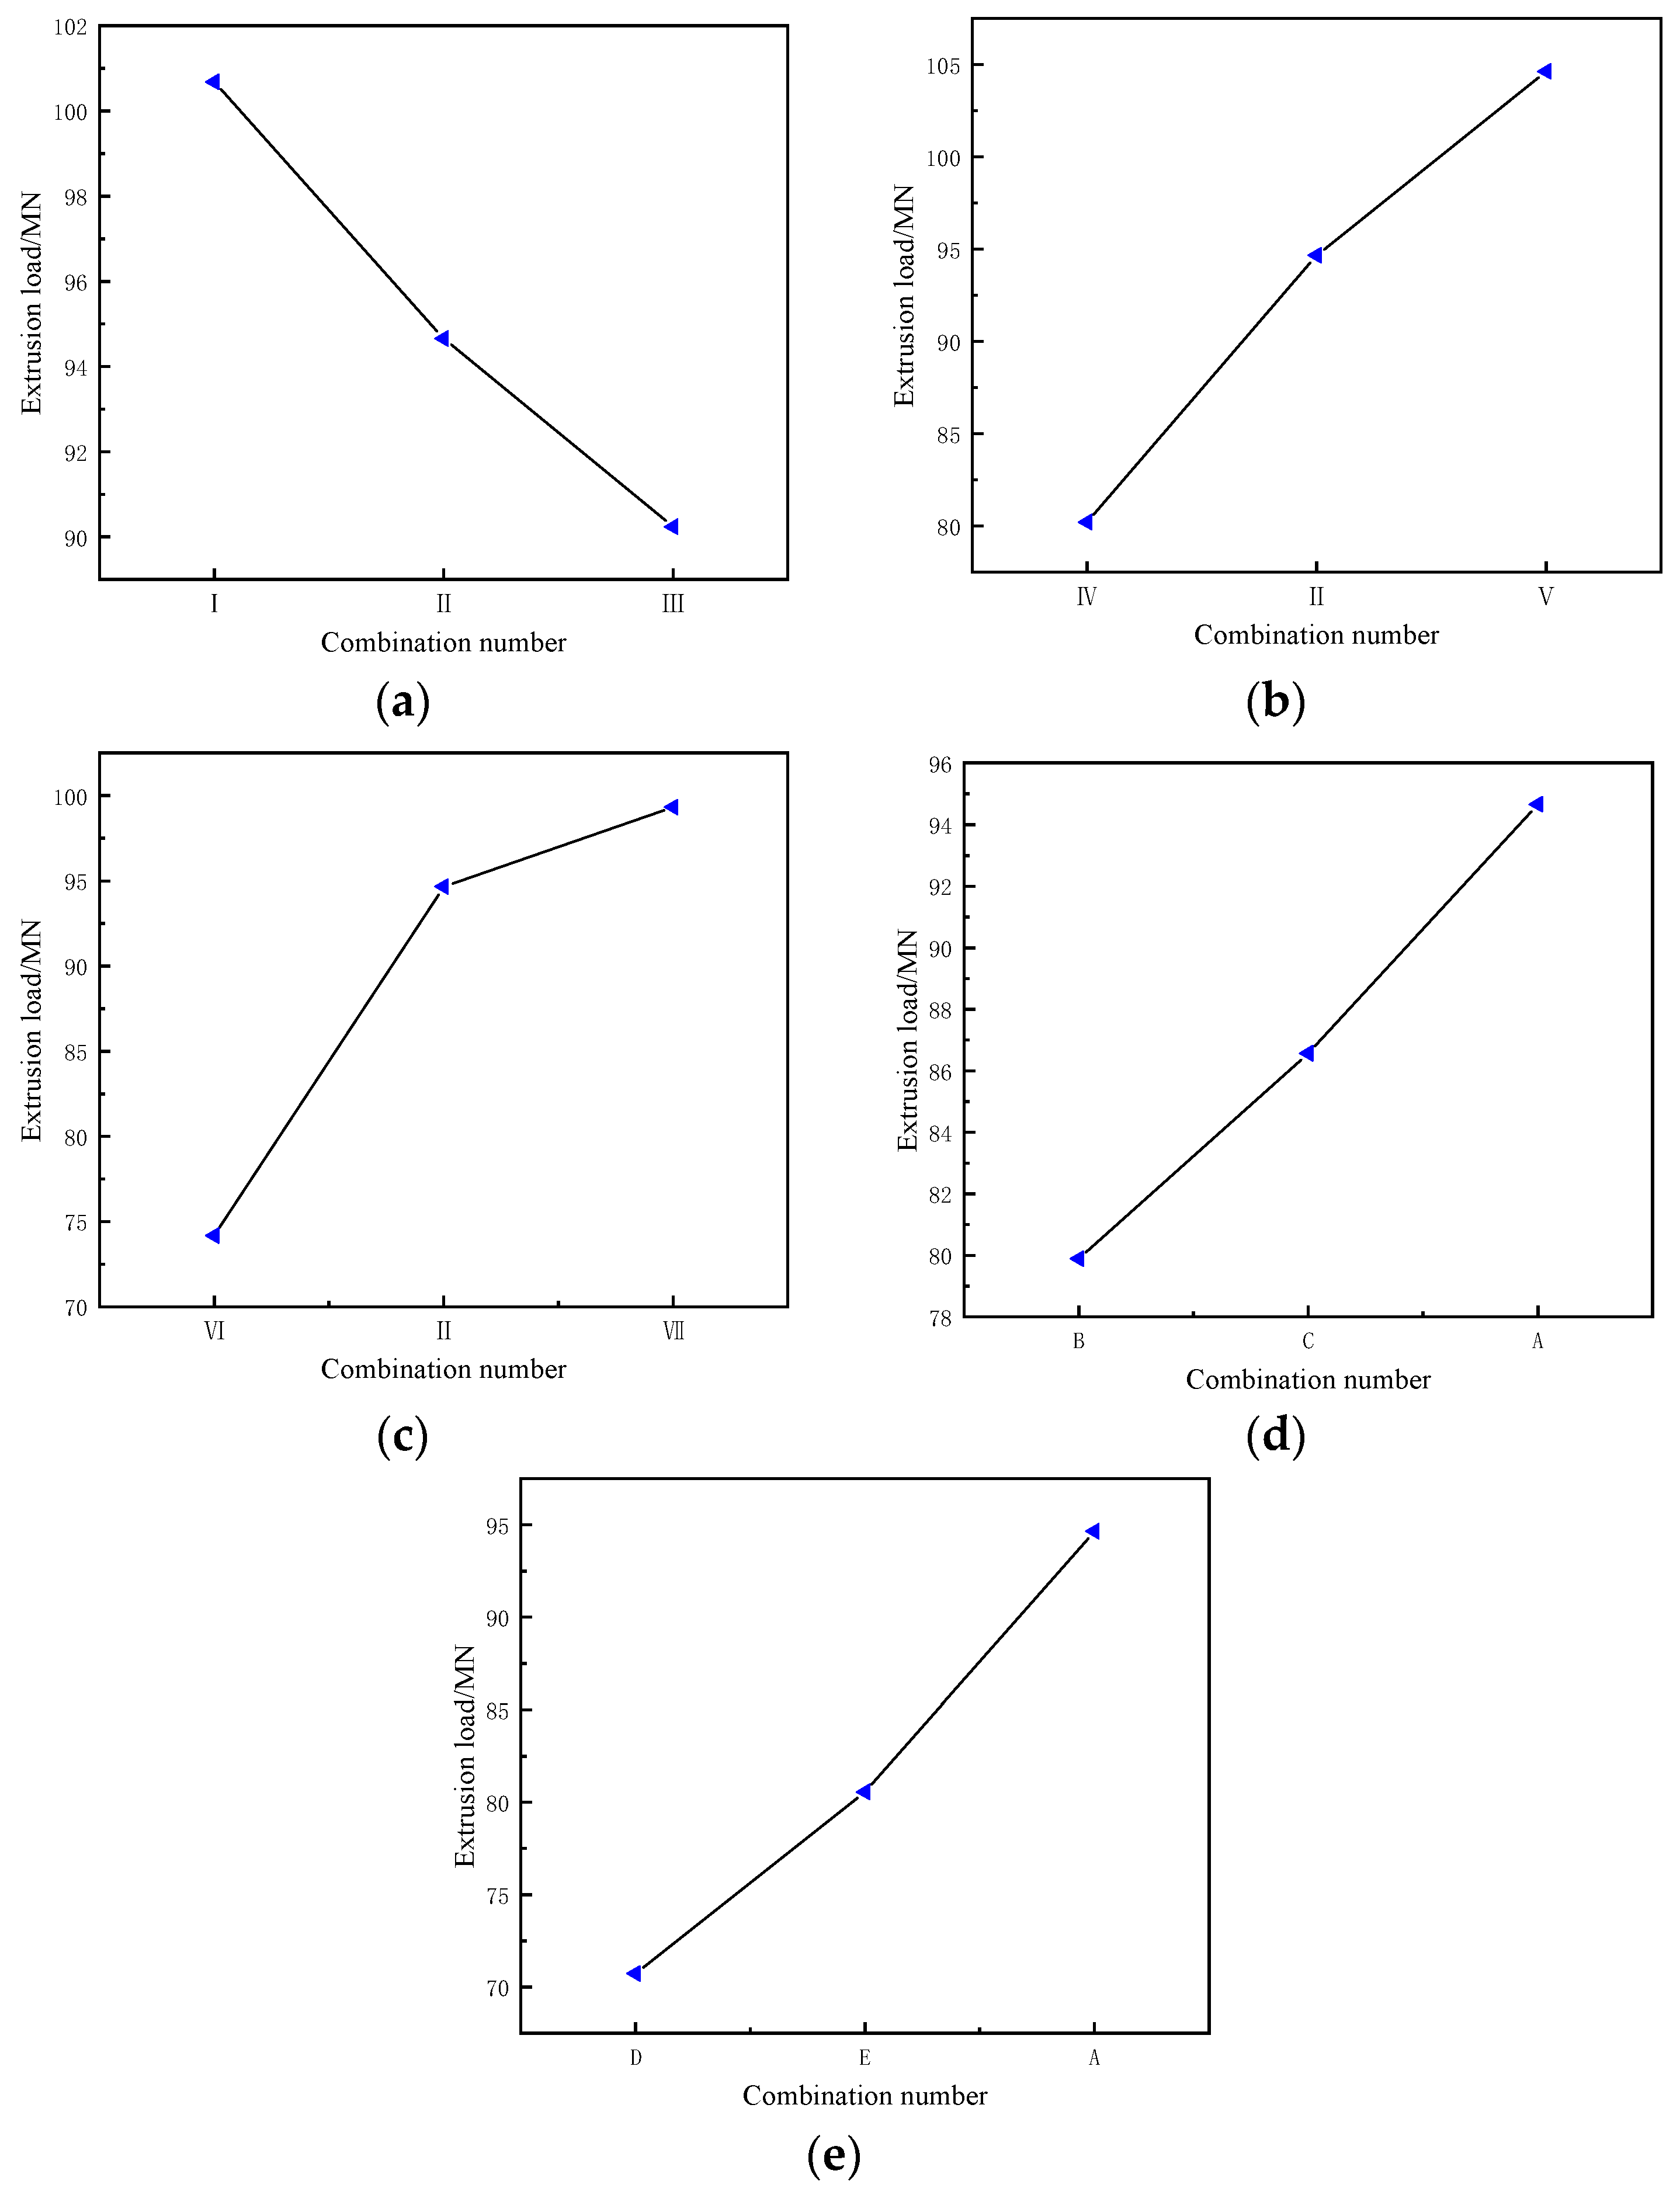
T, were set as 360 °C, 390 °C, and 420 °C. Based on the significant influence of the extrusion speed,
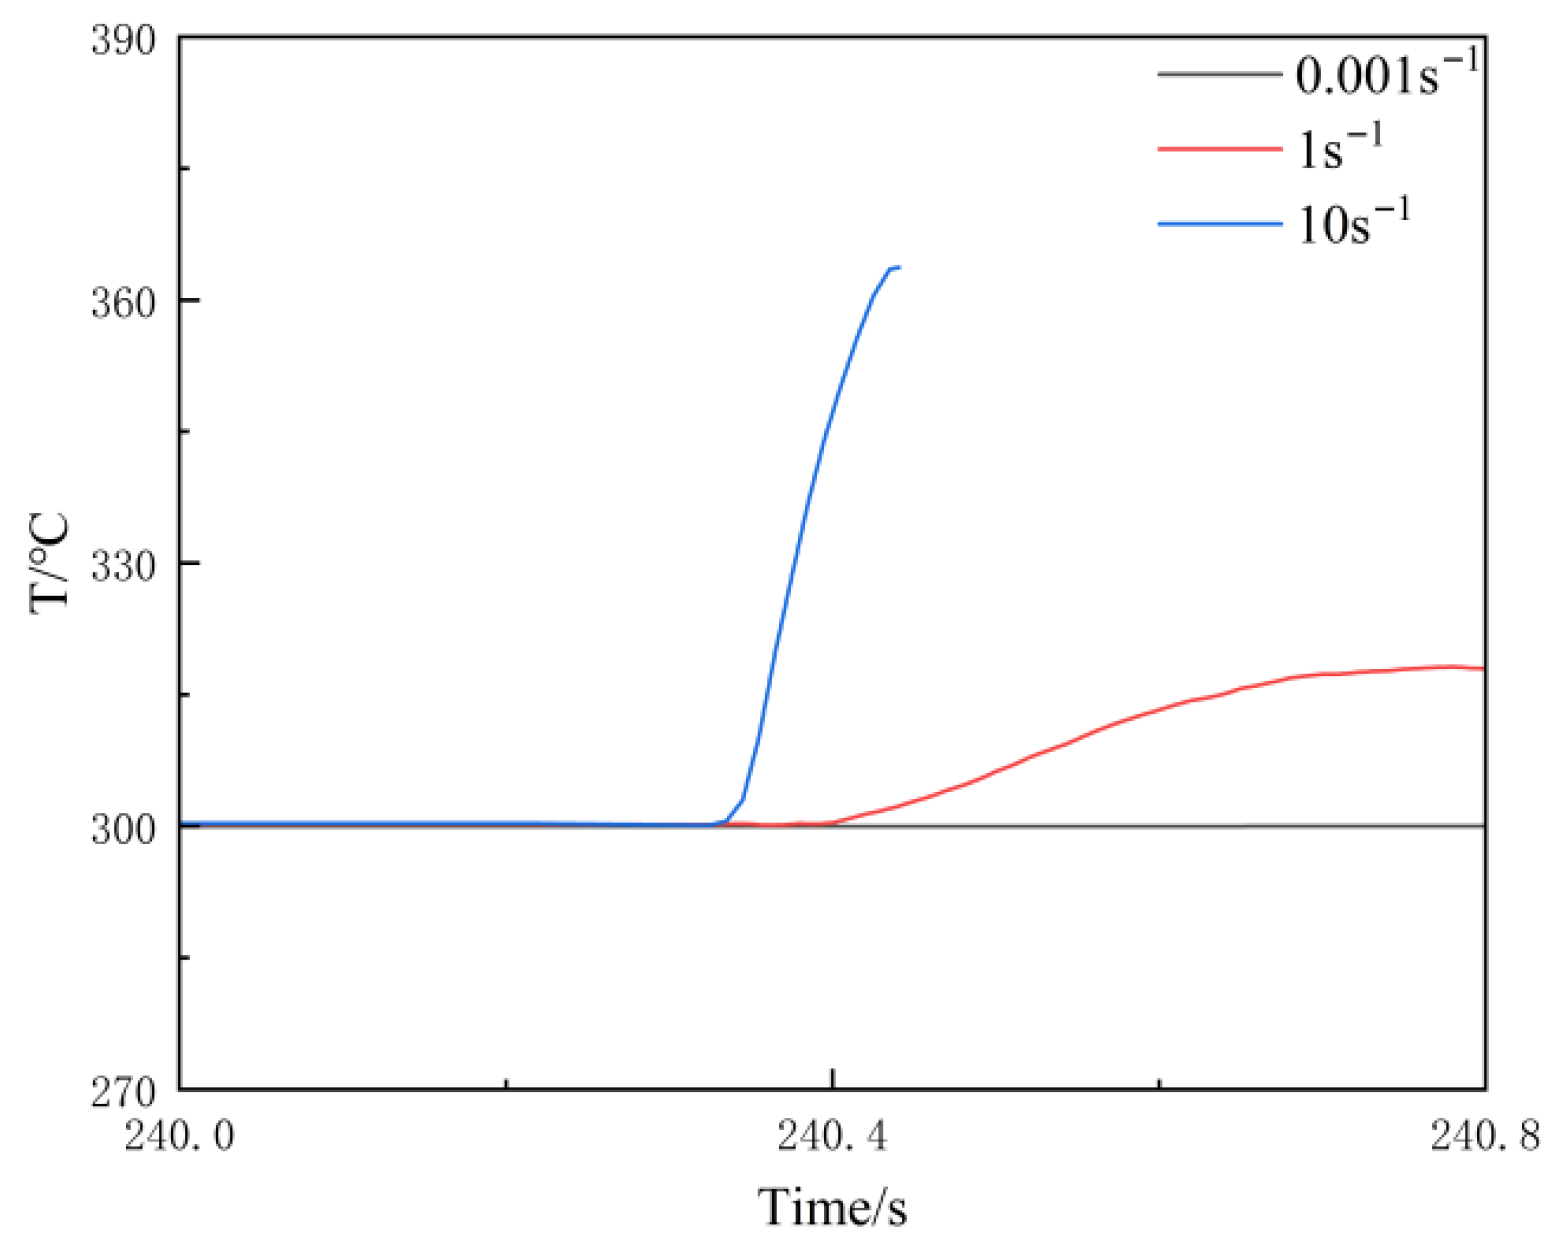
v, on the temperature of the extruded profile (
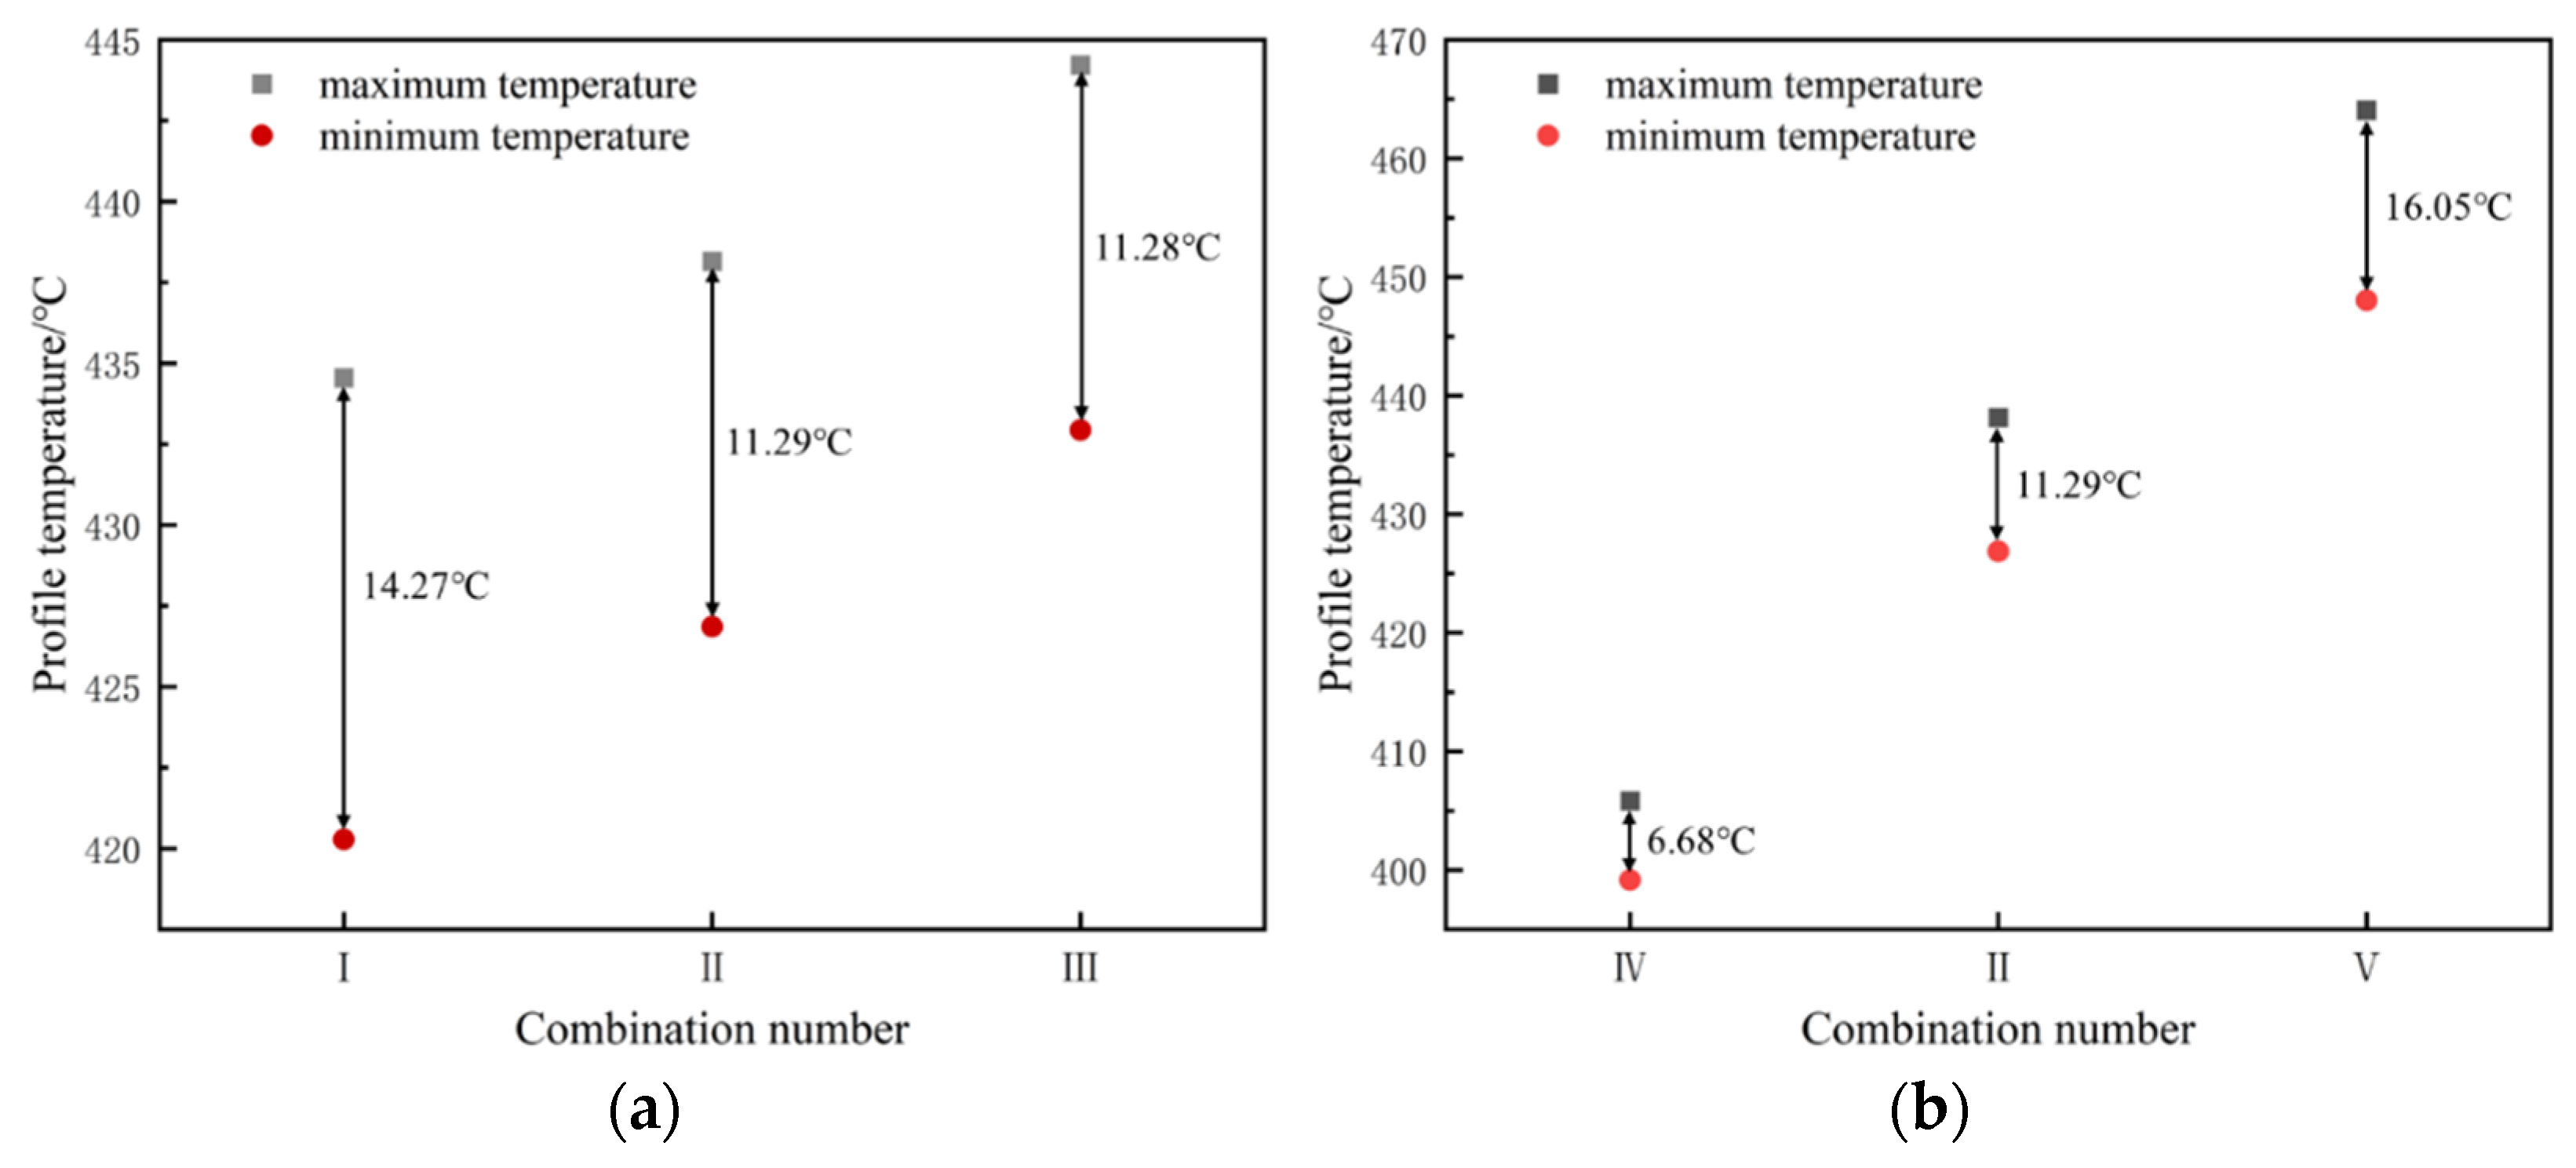
Figure 12b), and to prevent a scenario where the overburning temperature was exceeded, three levels of
v were designed: 0.1 mm/s, 0.3 mm/s, and 0.5 mm/s. Based on the capacity of the extrusion equipment, the three levels of the billet length,
L, design were 350 mm, 575 mm, and 800 mm, respectively.
3.5.3. Response Surface Model
The second-order response surface equation fitted by the least squares method is expressed as follows:
In this equation, is the design variable, is the residual error, and , , , and are all the undetermined coefficients.
Based on the data in
Table 6 and using Equation (15) as the base expression, the response surface functions of the extrusion load, F, the deviation value, VDD, of the profile cross-sectional velocity, the average strain,
, of the profile cross-section, and the temperature difference,
, of the profile cross-section with respect to each design variable are obtained, as shown in Equations (16)–(19):
The above four response surface models were used to predict, respectively, the four optimization objectives, F, VDD,
, and
, under different extrusion process parameters.
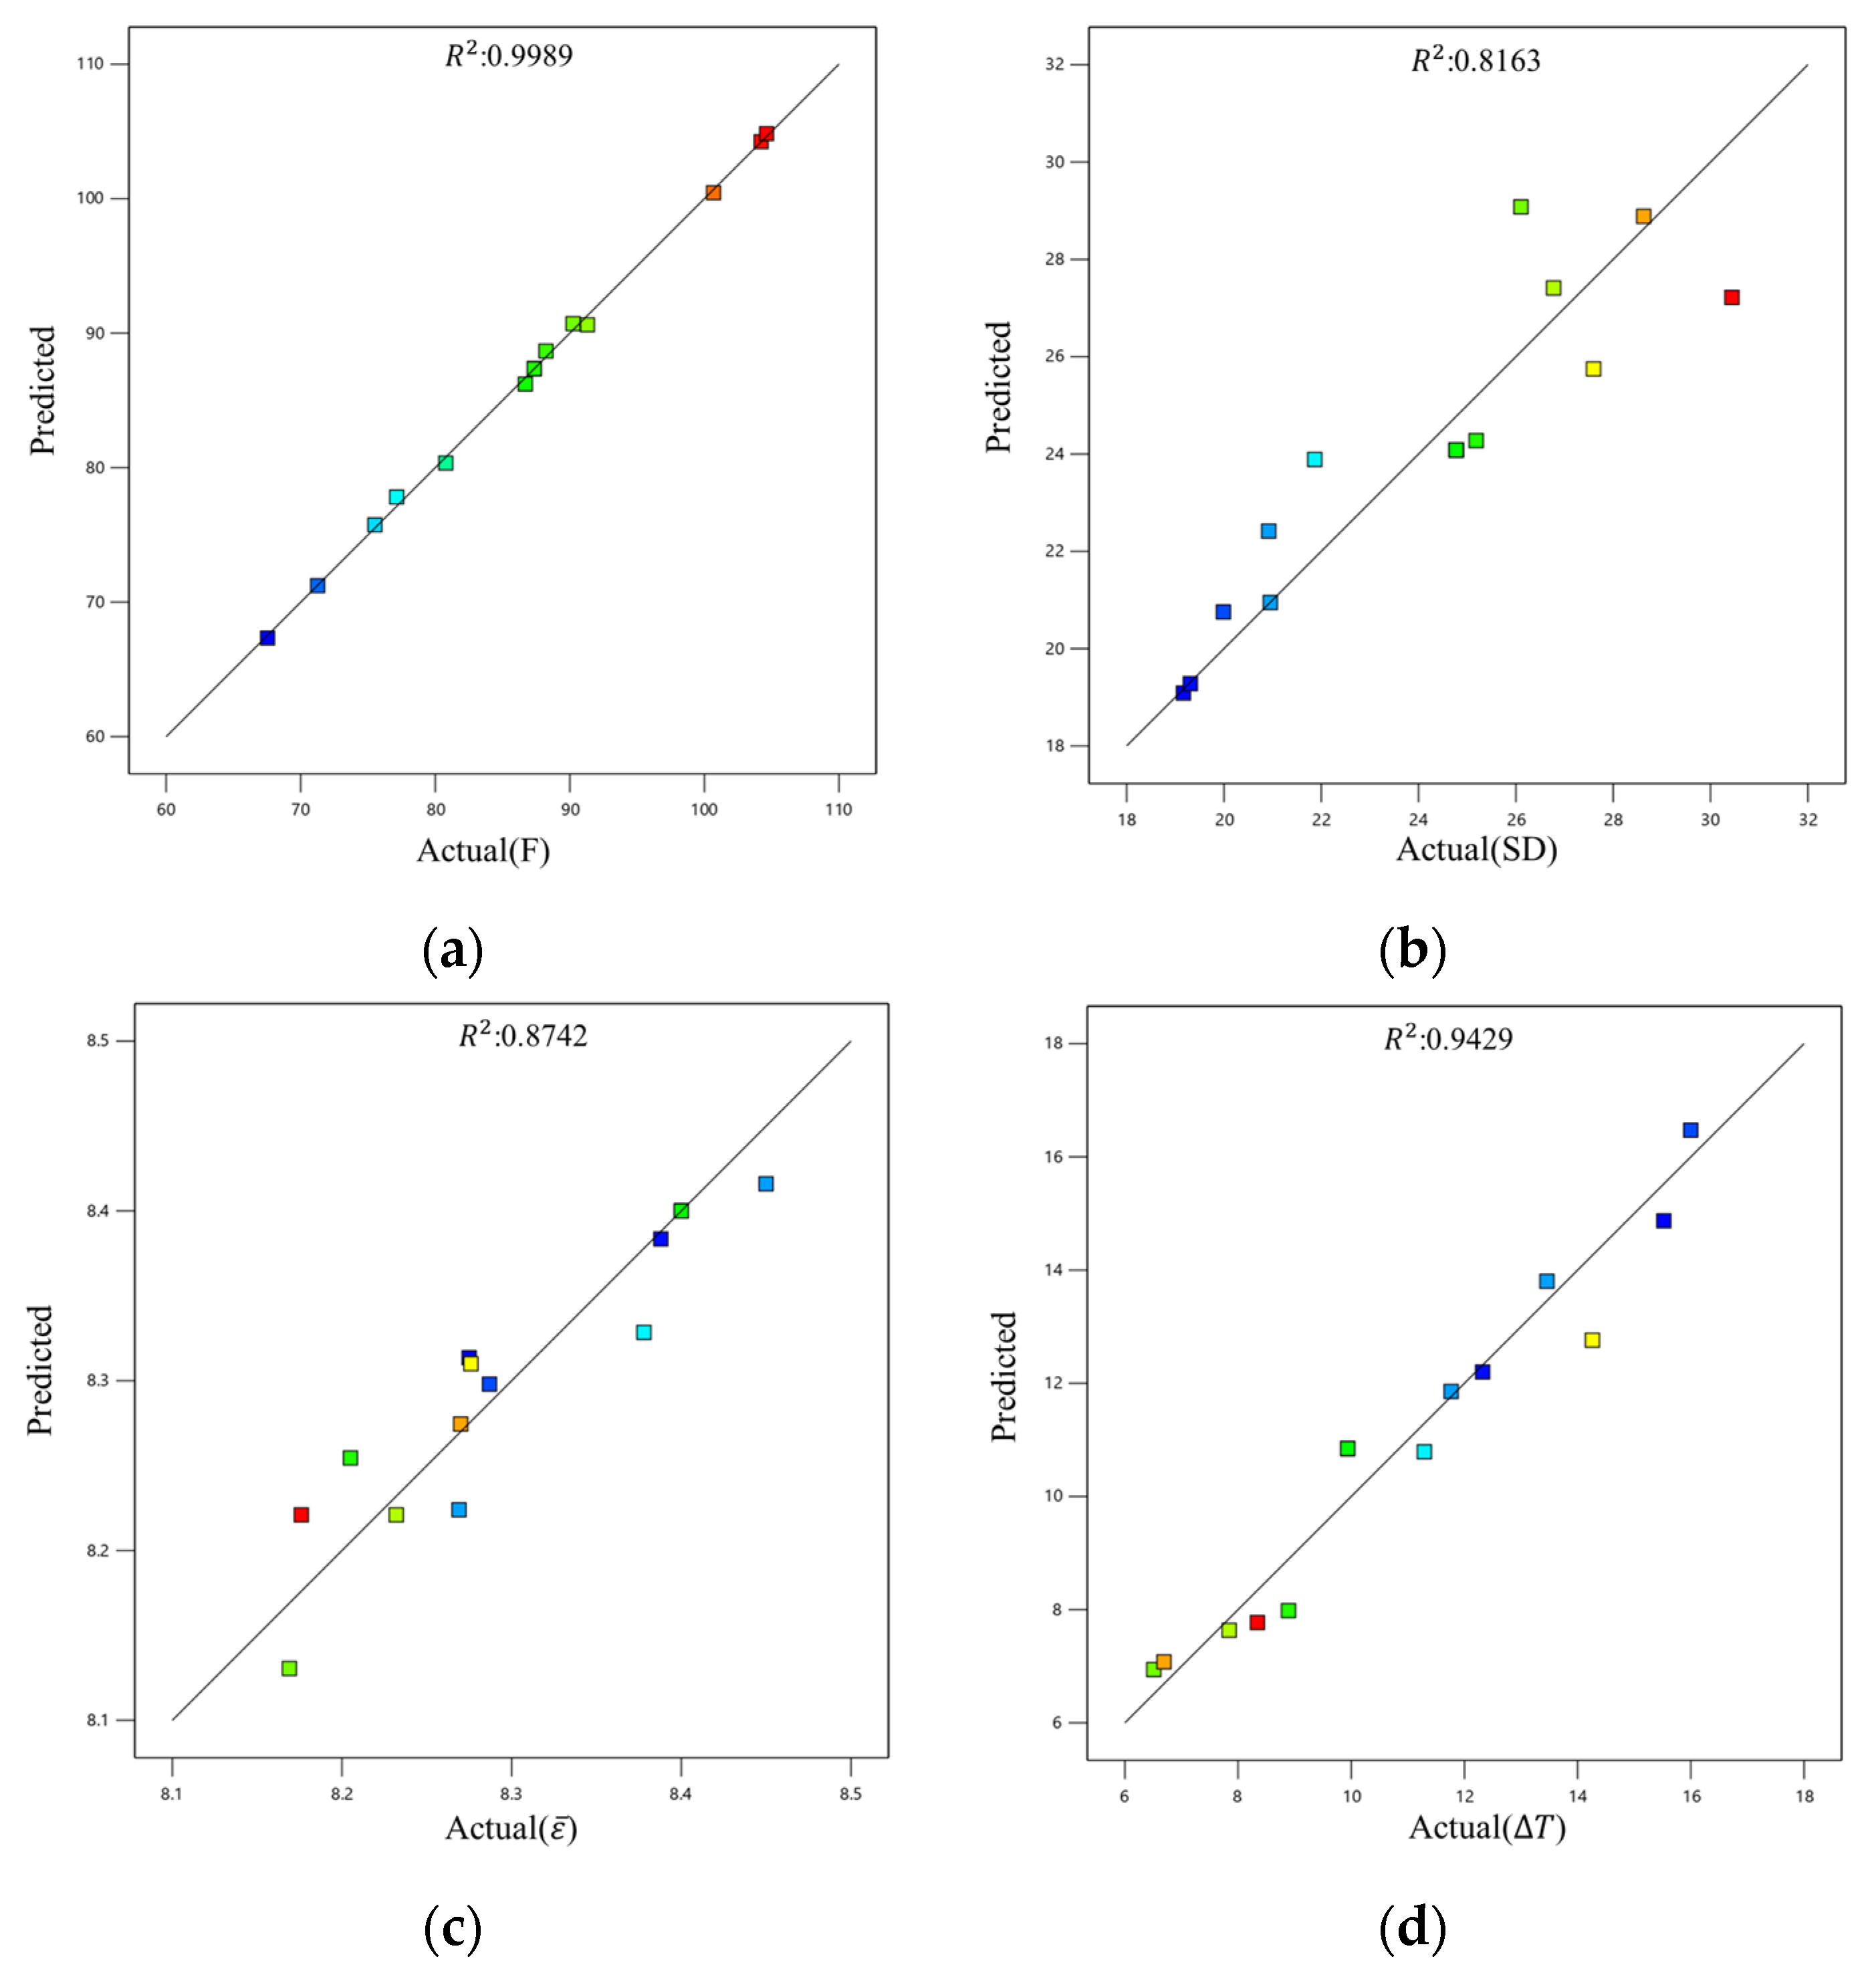
Figure 16 shows the comparison between the predicted values and actual values of the response surfaces for the various optimization objectives. Squares of different colors in the figure represent distinct actual data points.The results in
Figure 16a,d indicate that the predicted values of the extrusion load, F, and the temperature difference,
, of the profile cross-section are in good agreement with the actual values, suggesting that these response surface models are reliable.
Figure 16b,c indicate, however, that the predicted values of the velocity deviation difference, VDD, and the average strain,
, of the profile cross-section deviate significantly from the actual values, necessitating a significance test evaluation.
The significance tests were conducted on the response surface models for key response indicators (extrusion load, flow velocity deviation, average strain, and cross-sectional temperature difference). The complete analysis tables are provided in
Appendix A. The results indicate the following findings: The model for the extrusion load is highly statistically significant (F = 488.19,
p < 0.0001, R
2 = 0.9989). Among the factors, the extrusion speed (
v) is the most influential factor affecting the extrusion load. The model for flow velocity deviation is statistically significant (F = 16.30,
p = 0.0002). Its variation is primarily driven by extrusion speed (v). The model for average strain did not pass the significance test (
p = 0.0754 > 0.05). This indicates that, within the range of process parameters studied, the billet temperature (
T), extrusion speed (
v), and ingot length (
L) have no significant impact on the average strain across the profile cross-section. The model for cross-sectional temperature difference is statistically significant (F = 22.00,
p < 0.0001). Extrusion speed (
v) is again the most significant factor contributing to the cross-sectional temperature difference.
3.5.4. Response Surface Analysis
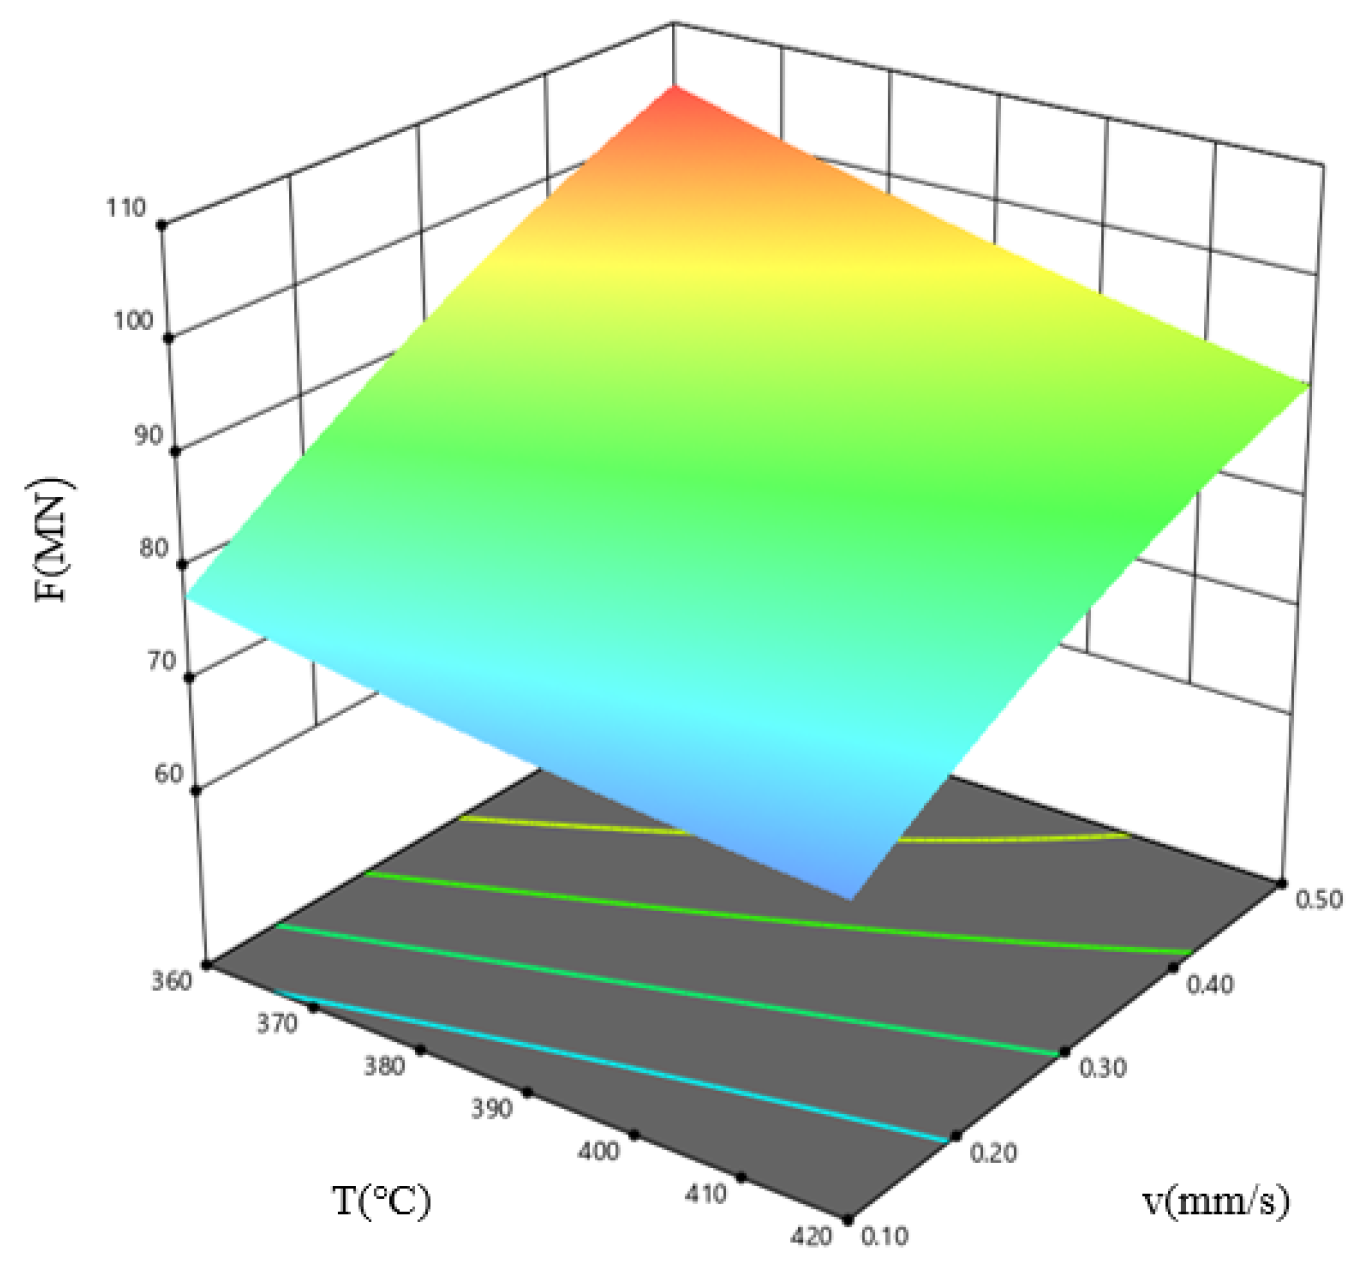
Figure 17 shows the response surface plot for the combined influence of billet temperature,
T, and extrusion speed,
v, on the extrusion load, F, when the ingot length,
L, is 575 mm. The results indicate that the extrusion load is minimal within the high-temperature, low-speed parameter window. As the billet temperature increases, the metal deformation resistance decreases, the plasticity increases, and the extrusion load decreases; at lower extrusion speeds, metal deformation occurs more slowly, internal stresses have time to adjust, the deformation heat effect is not significant, the temperature changes are smooth, and the metal deformation resistance is lower than at high speeds, resulting in reduced extrusion load.
Figure 18 shows the response surface plot for the combined influence of the billet temperature,
T, and ingot length,
L, on F at an extrusion speed,
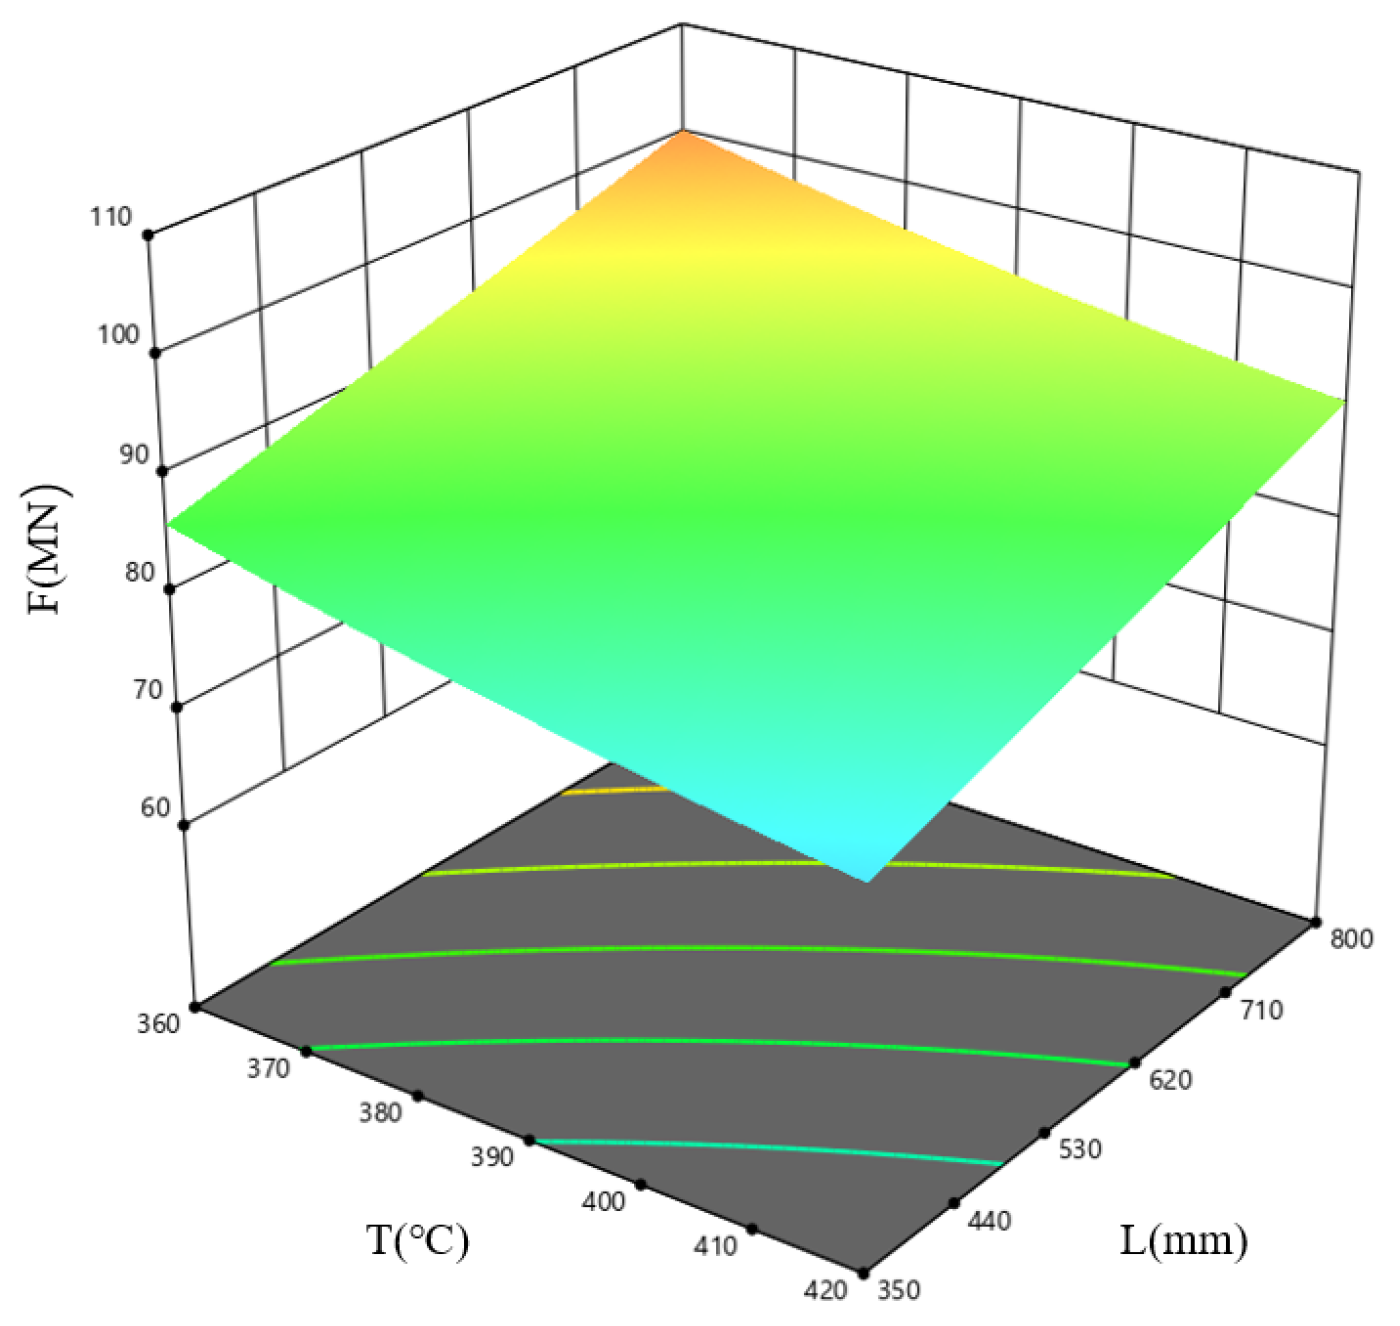
v, of 0.3 mm/s. The results indicate that the extrusion load is minimal within the high-temperature, short-ingot-length parameter window. As the ingot length increases, the contact area with the extrusion cylinder increases, the friction increases, the metal flow path lengthens, the flow resistance increases, and the pressure required to break through the extrusion increases.
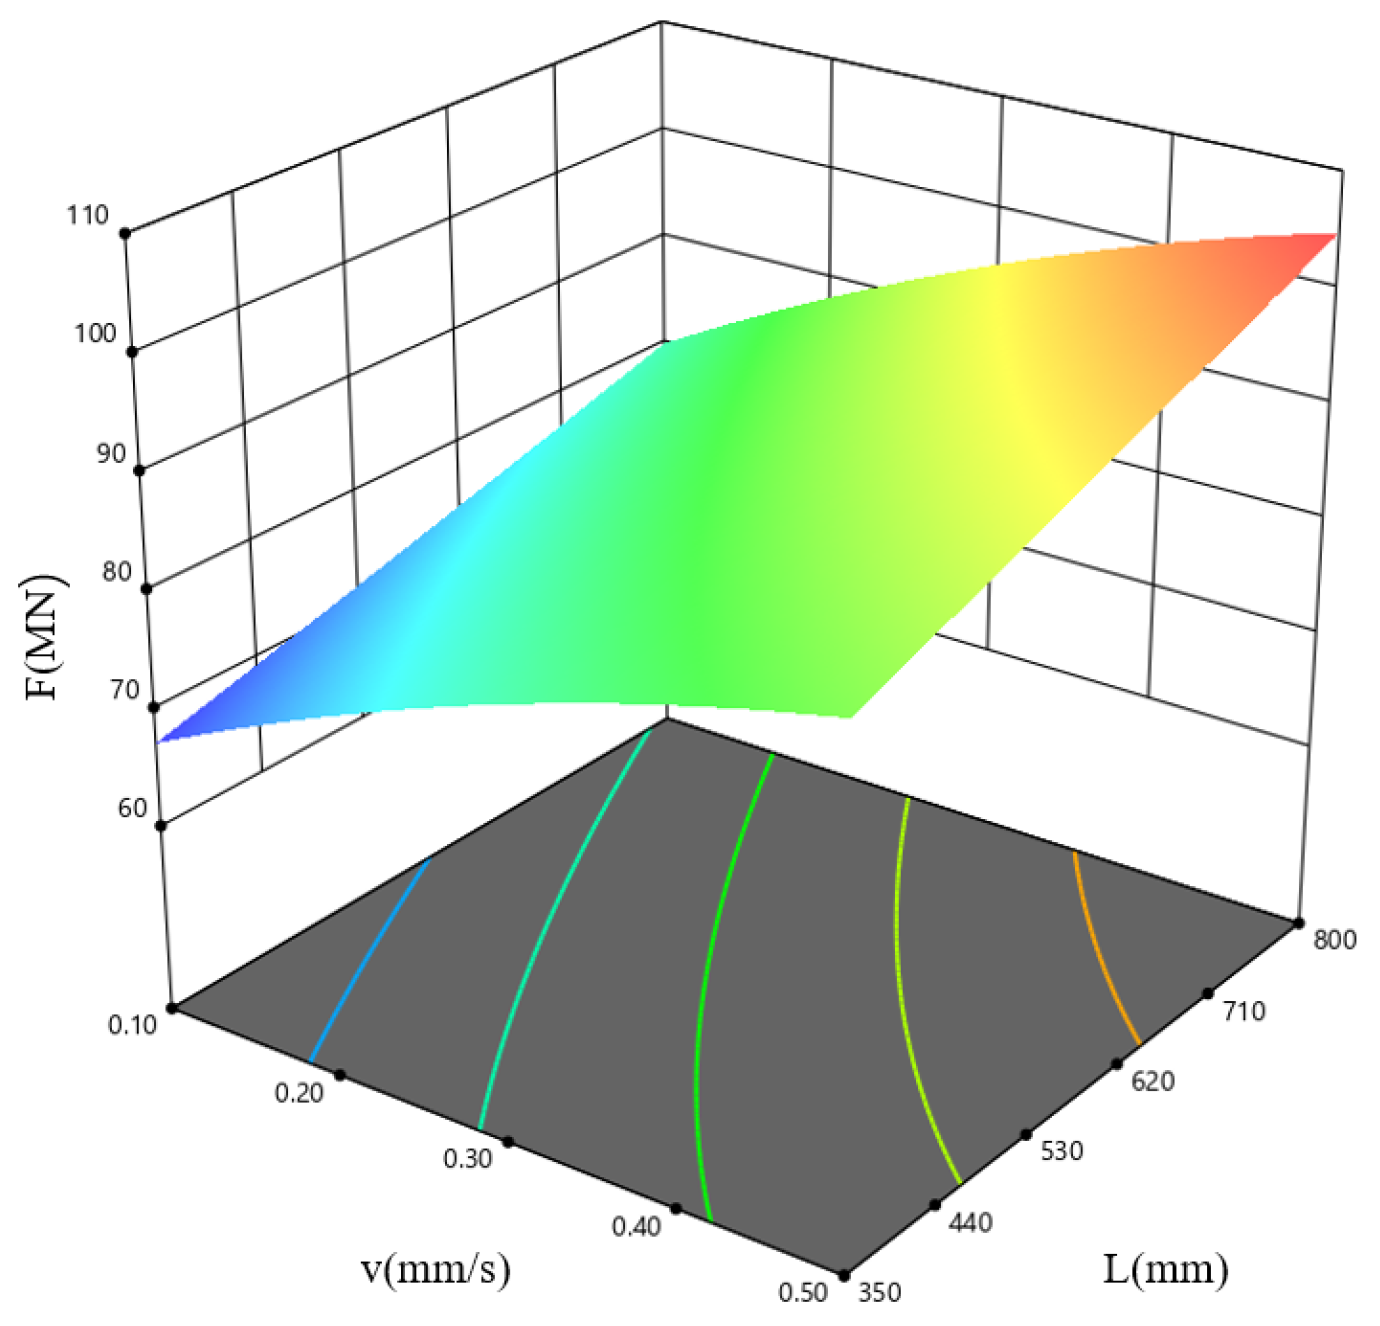
Figure 19 shows the response surface plot for the combined influence of the extrusion speed,
v, and the ingot length,
L, on F at a billet temperature,
T, equal to 390 °C. The results indicate that the extrusion load is minimal within the low-speed, short-ingot-length parameter window.
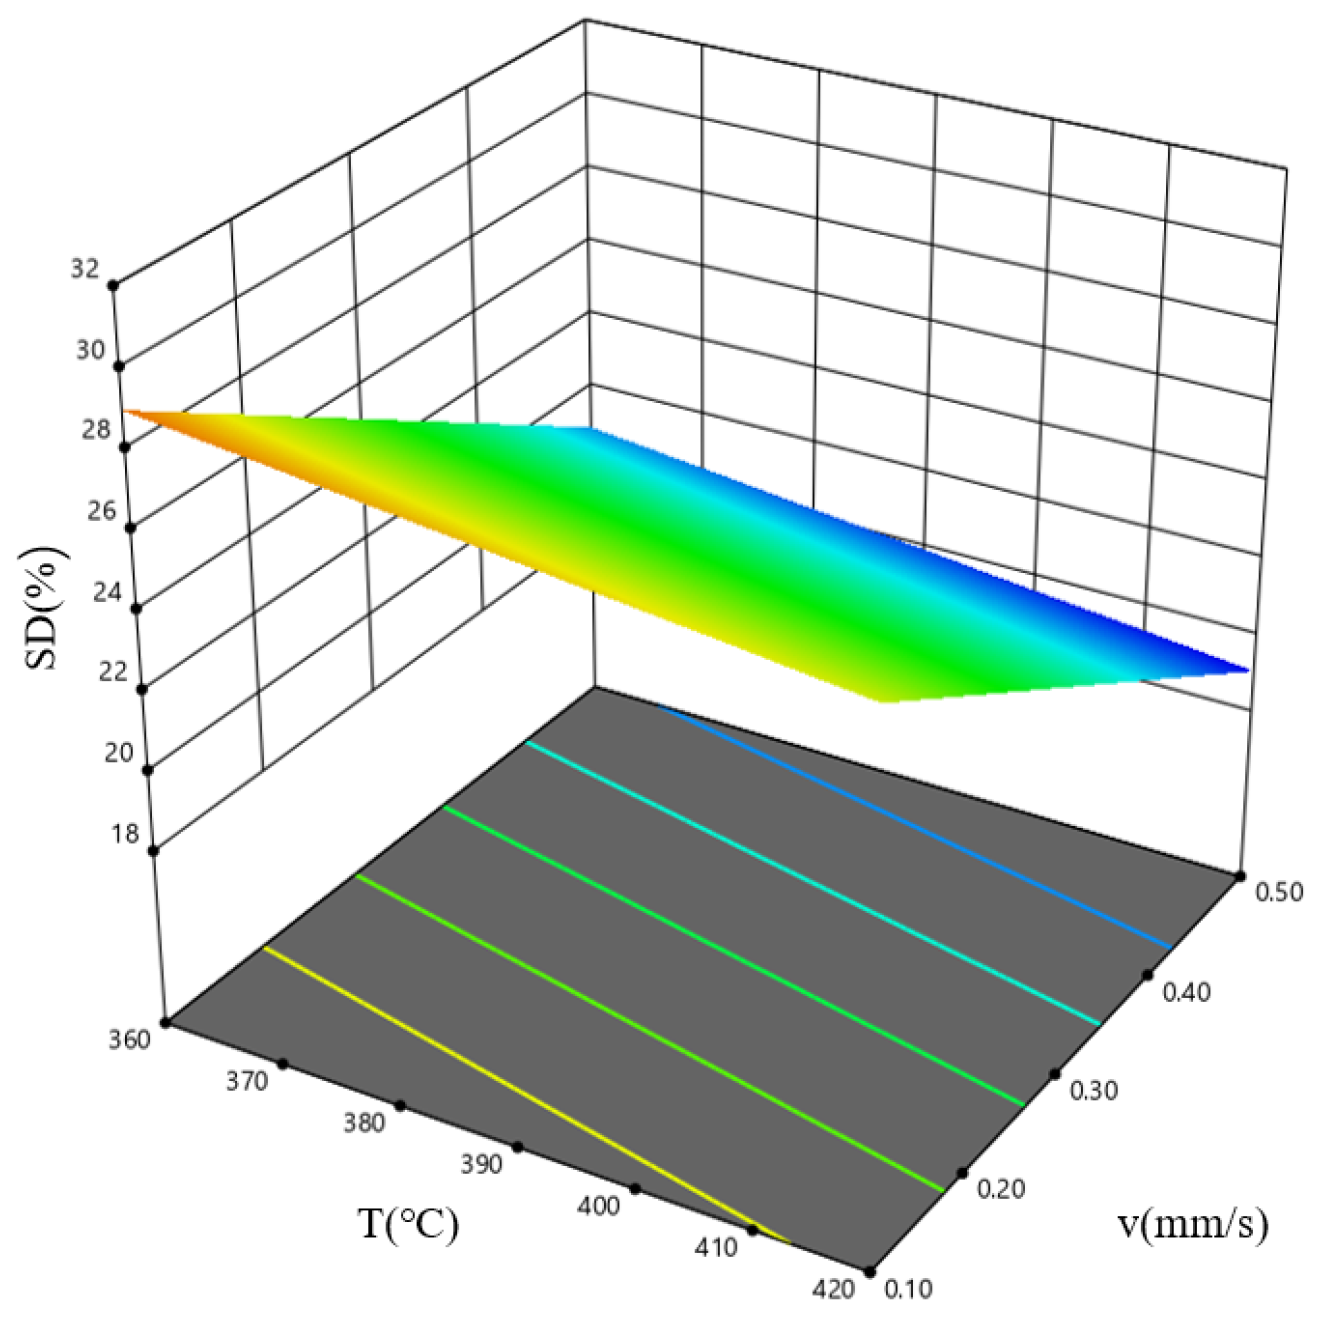
Figure 20 shows the response surface plot for the combined influence of the billet temperature,
T, and the extrusion speed,
v, on the speed deviation difference, VDD, when the ingot length,
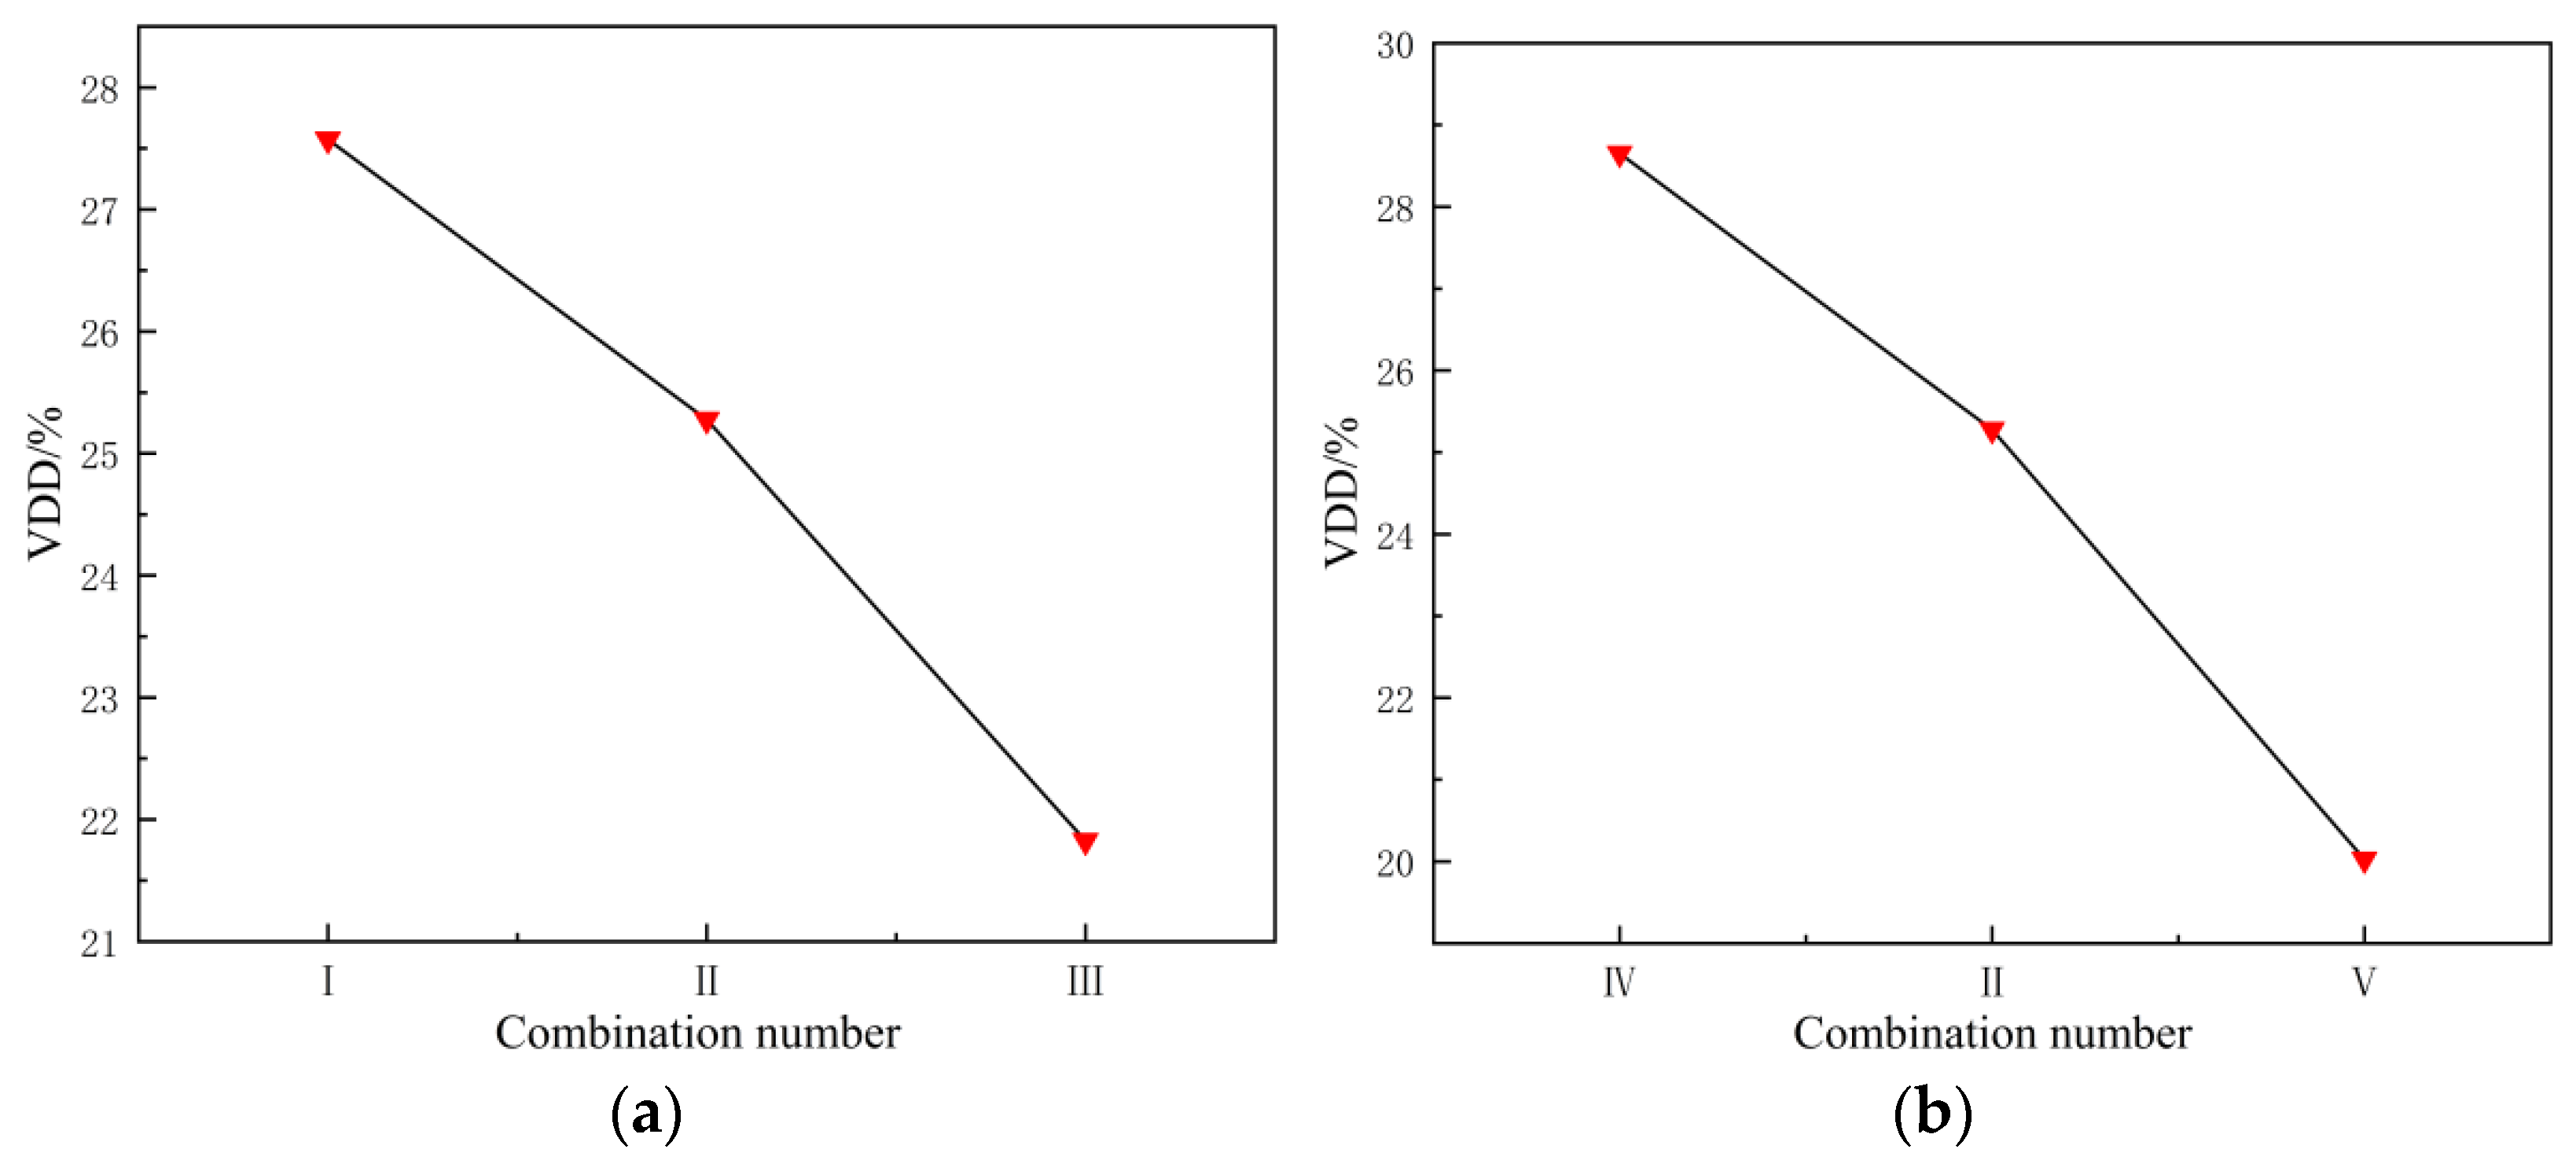
L, is 575 mm. The results indicate that, within the high-temperature, high-speed parameter window, the speed deviation difference in the extruded profile cross-section is minimal, and the flow velocity is most uniform. As the billet temperature decreases, the metal deformation resistance increases, the plasticity decreases, the deformation becomes uneven, and the velocity deviation difference increases. As the extrusion speed decreases, the metal flow slows down, the flow time increases, and the accumulation of uneven deformation makes the uneven deformation more pronounced, resulting in an increase in the velocity deviation difference.
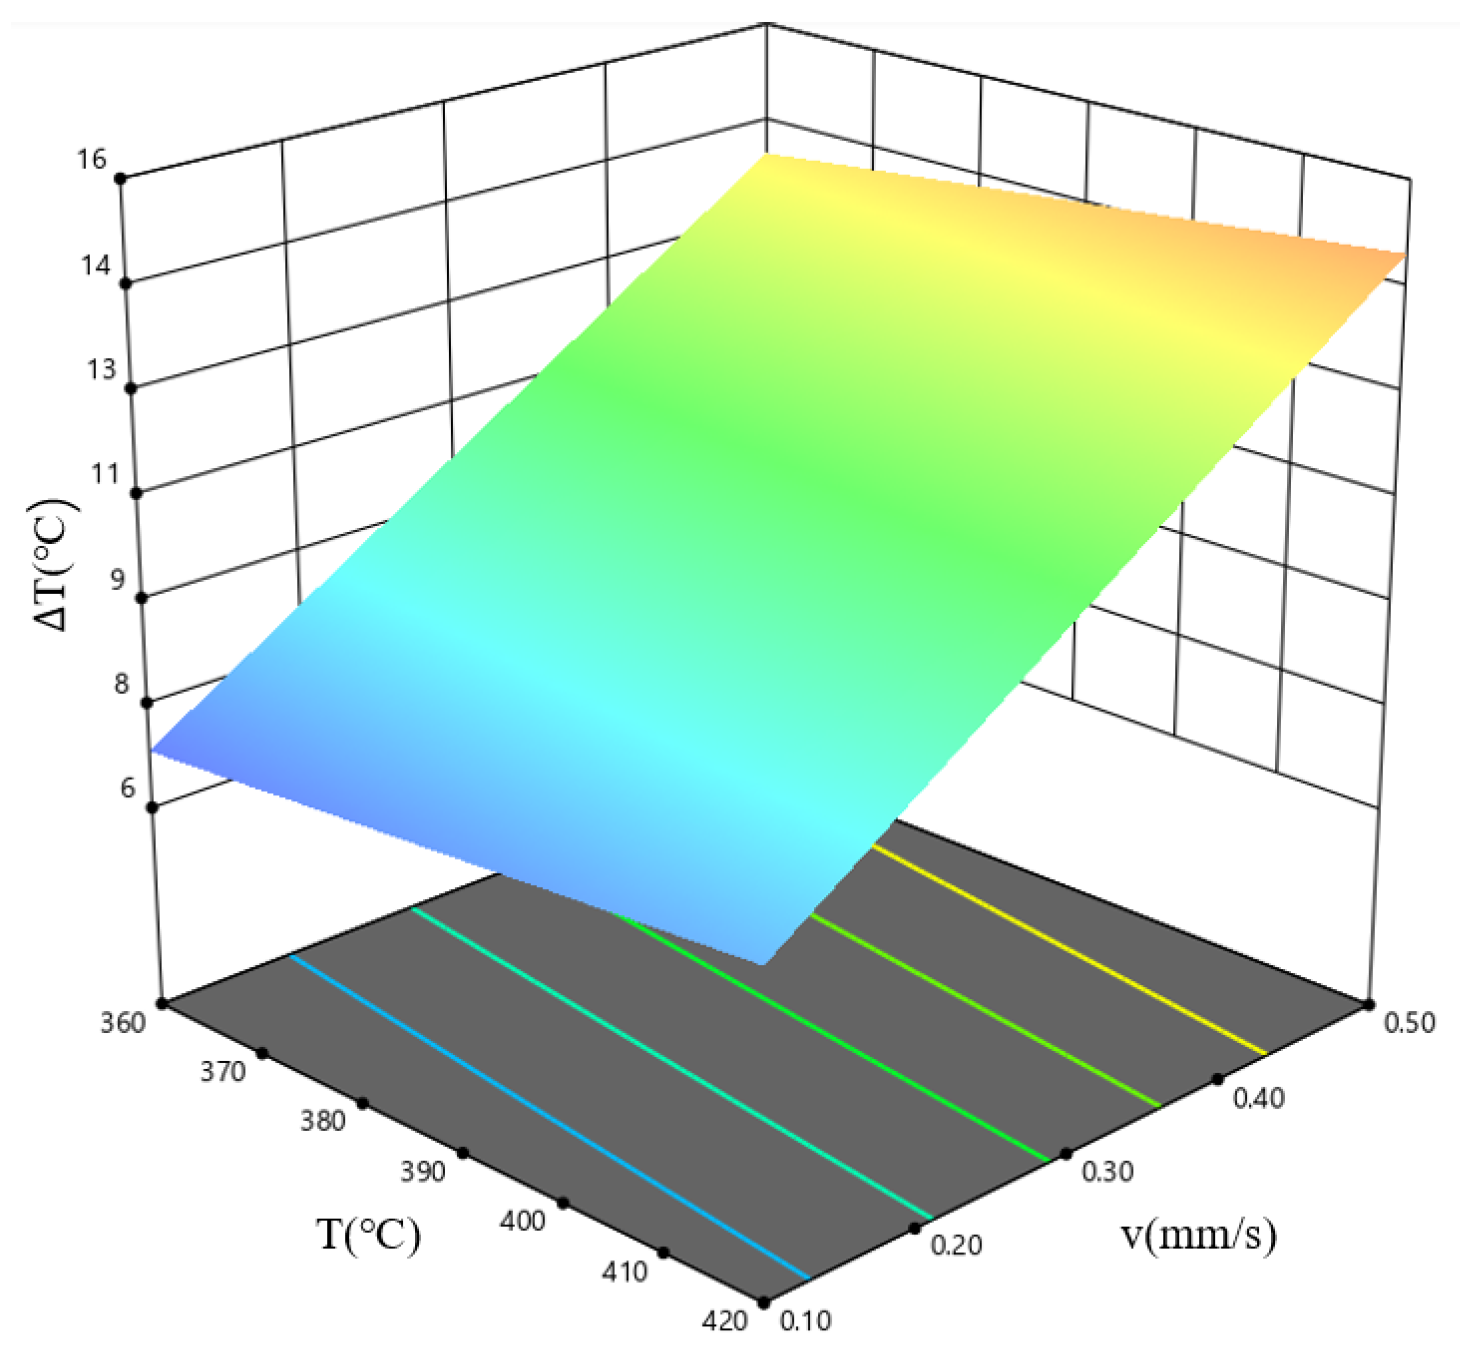
Figure 21 presents the response surface diagram for the combined influence of the billet temperature,
T, and the extrusion speed,
v, on the temperature difference,
, of the extruded profile, when the ingot length,
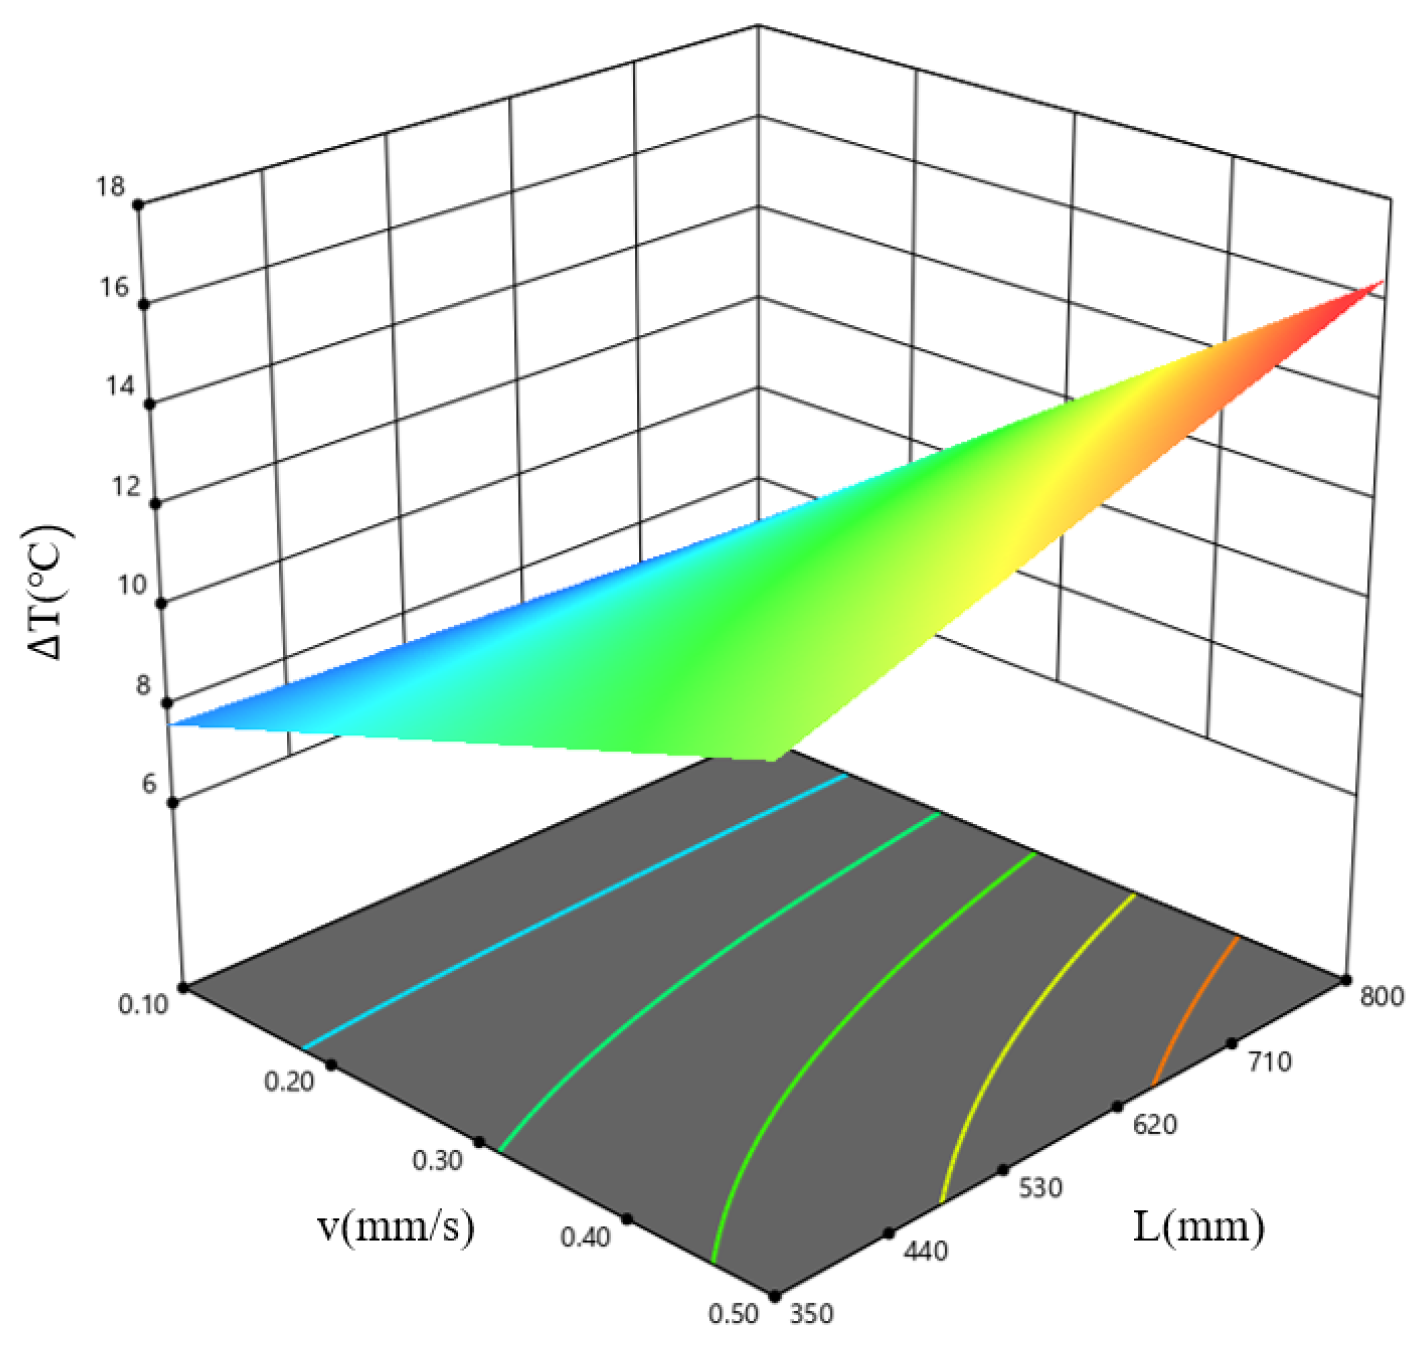
L, is 575 mm. The results indicate that the temperature difference across the extruded profile cross-section is minimal within the high-temperature, low-speed parameter window. As the billet temperature increases, the metal deformation resistance decreases, resulting in less deformation-induced heat generation and a smaller temperature difference across the extruded profile cross-section. Conversely, as the extrusion speed decreases, heat conduction becomes more uniform, leading to more balanced heat distribution and a smaller temperature difference across the extruded profile’s cross-section.
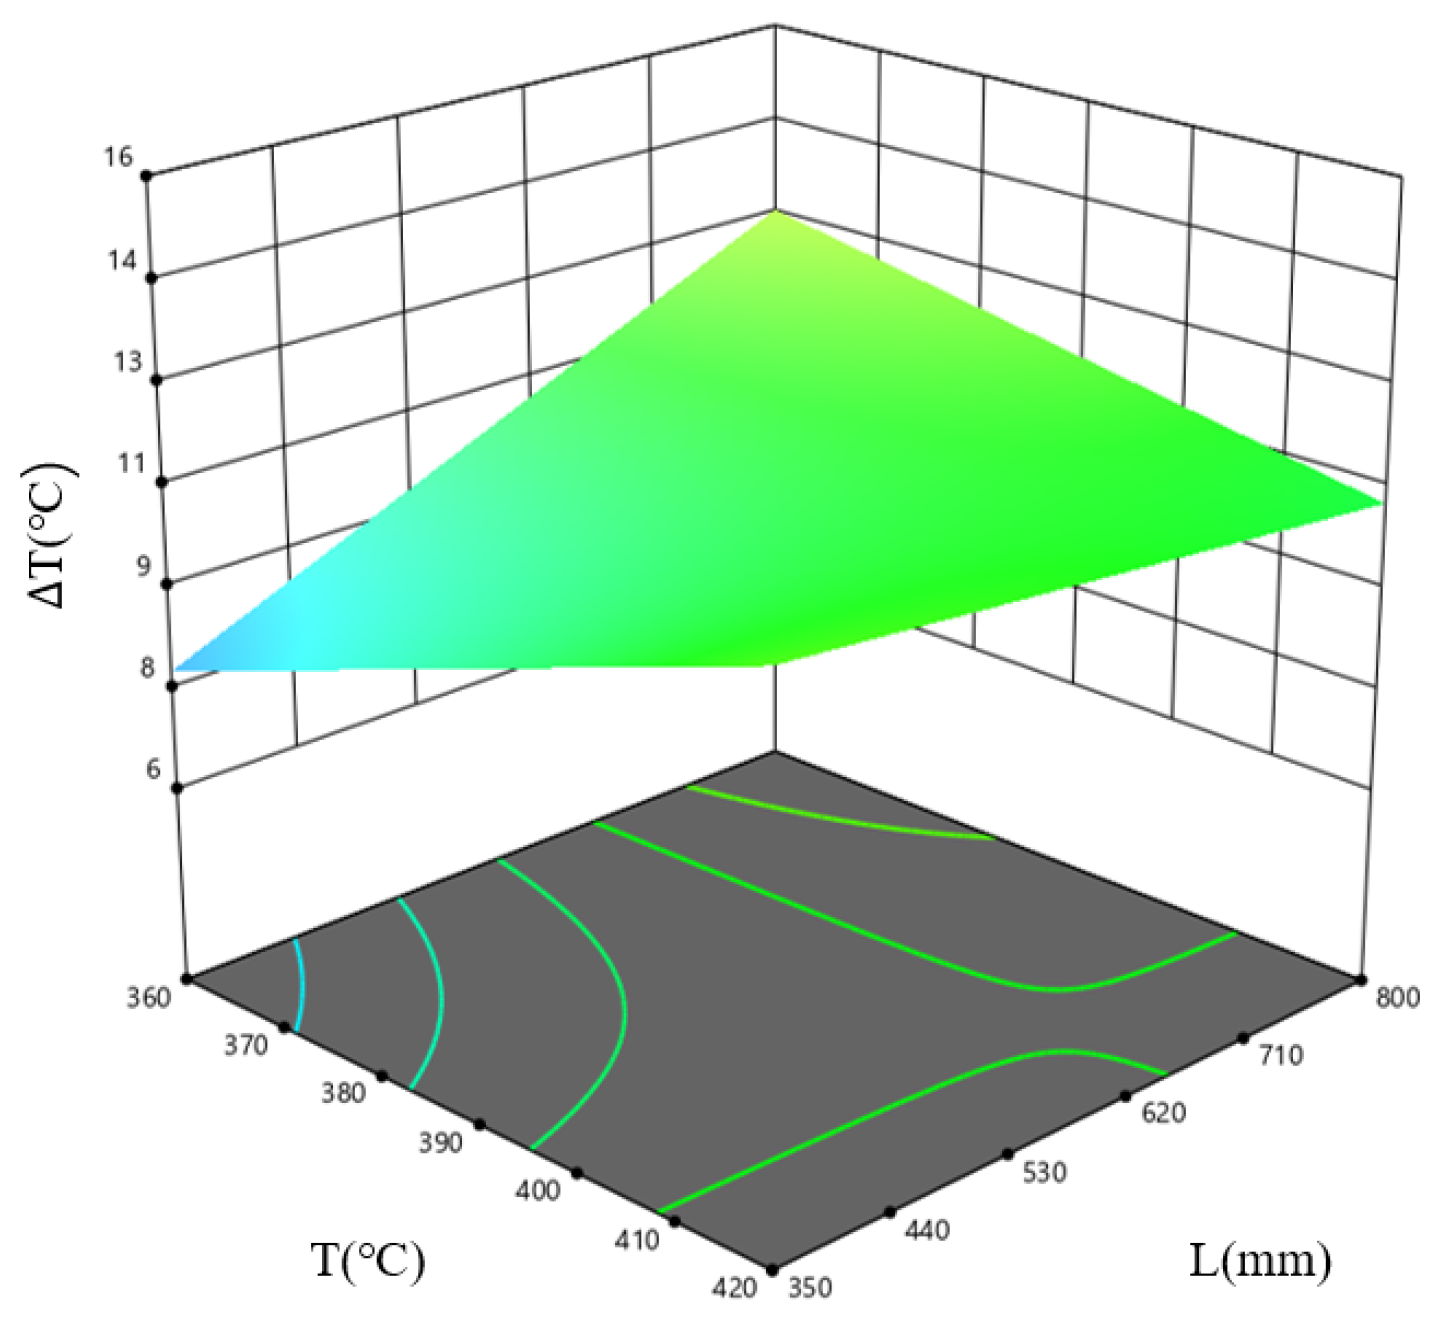
Figure 22 shows the response surface plot for the combined influence of the billet temperature,
T, and ingot length,
L, on
at an extrusion speed,
v, of 0.3 mm/s. The results indicate that this temperature difference is minimal within the low-temperature, short-ingot-length parameter window. This is because, as ingot length increases, the distance for heat conduction increases, leading to uneven heat distribution and a larger temperature difference across the profile cross-section; the lower the billet temperature, the lower the heat conduction capacity, resulting in less deformation-induced heat generation and a larger temperature gradient. This leads to the billet length having a more significant influence on the temperature difference across the profile cross-section.
Figure 23 shows the response surface diagram for the combined influence of the extrusion speed,
v, and the ingot length,
L, on
when the billet temperature,
T, is 390 °C. The results indicate that the temperature difference in the cross-section of the extruded profile is minimal within the low-speed, short-ingot-length parameter window, consistent with the previous conclusion.
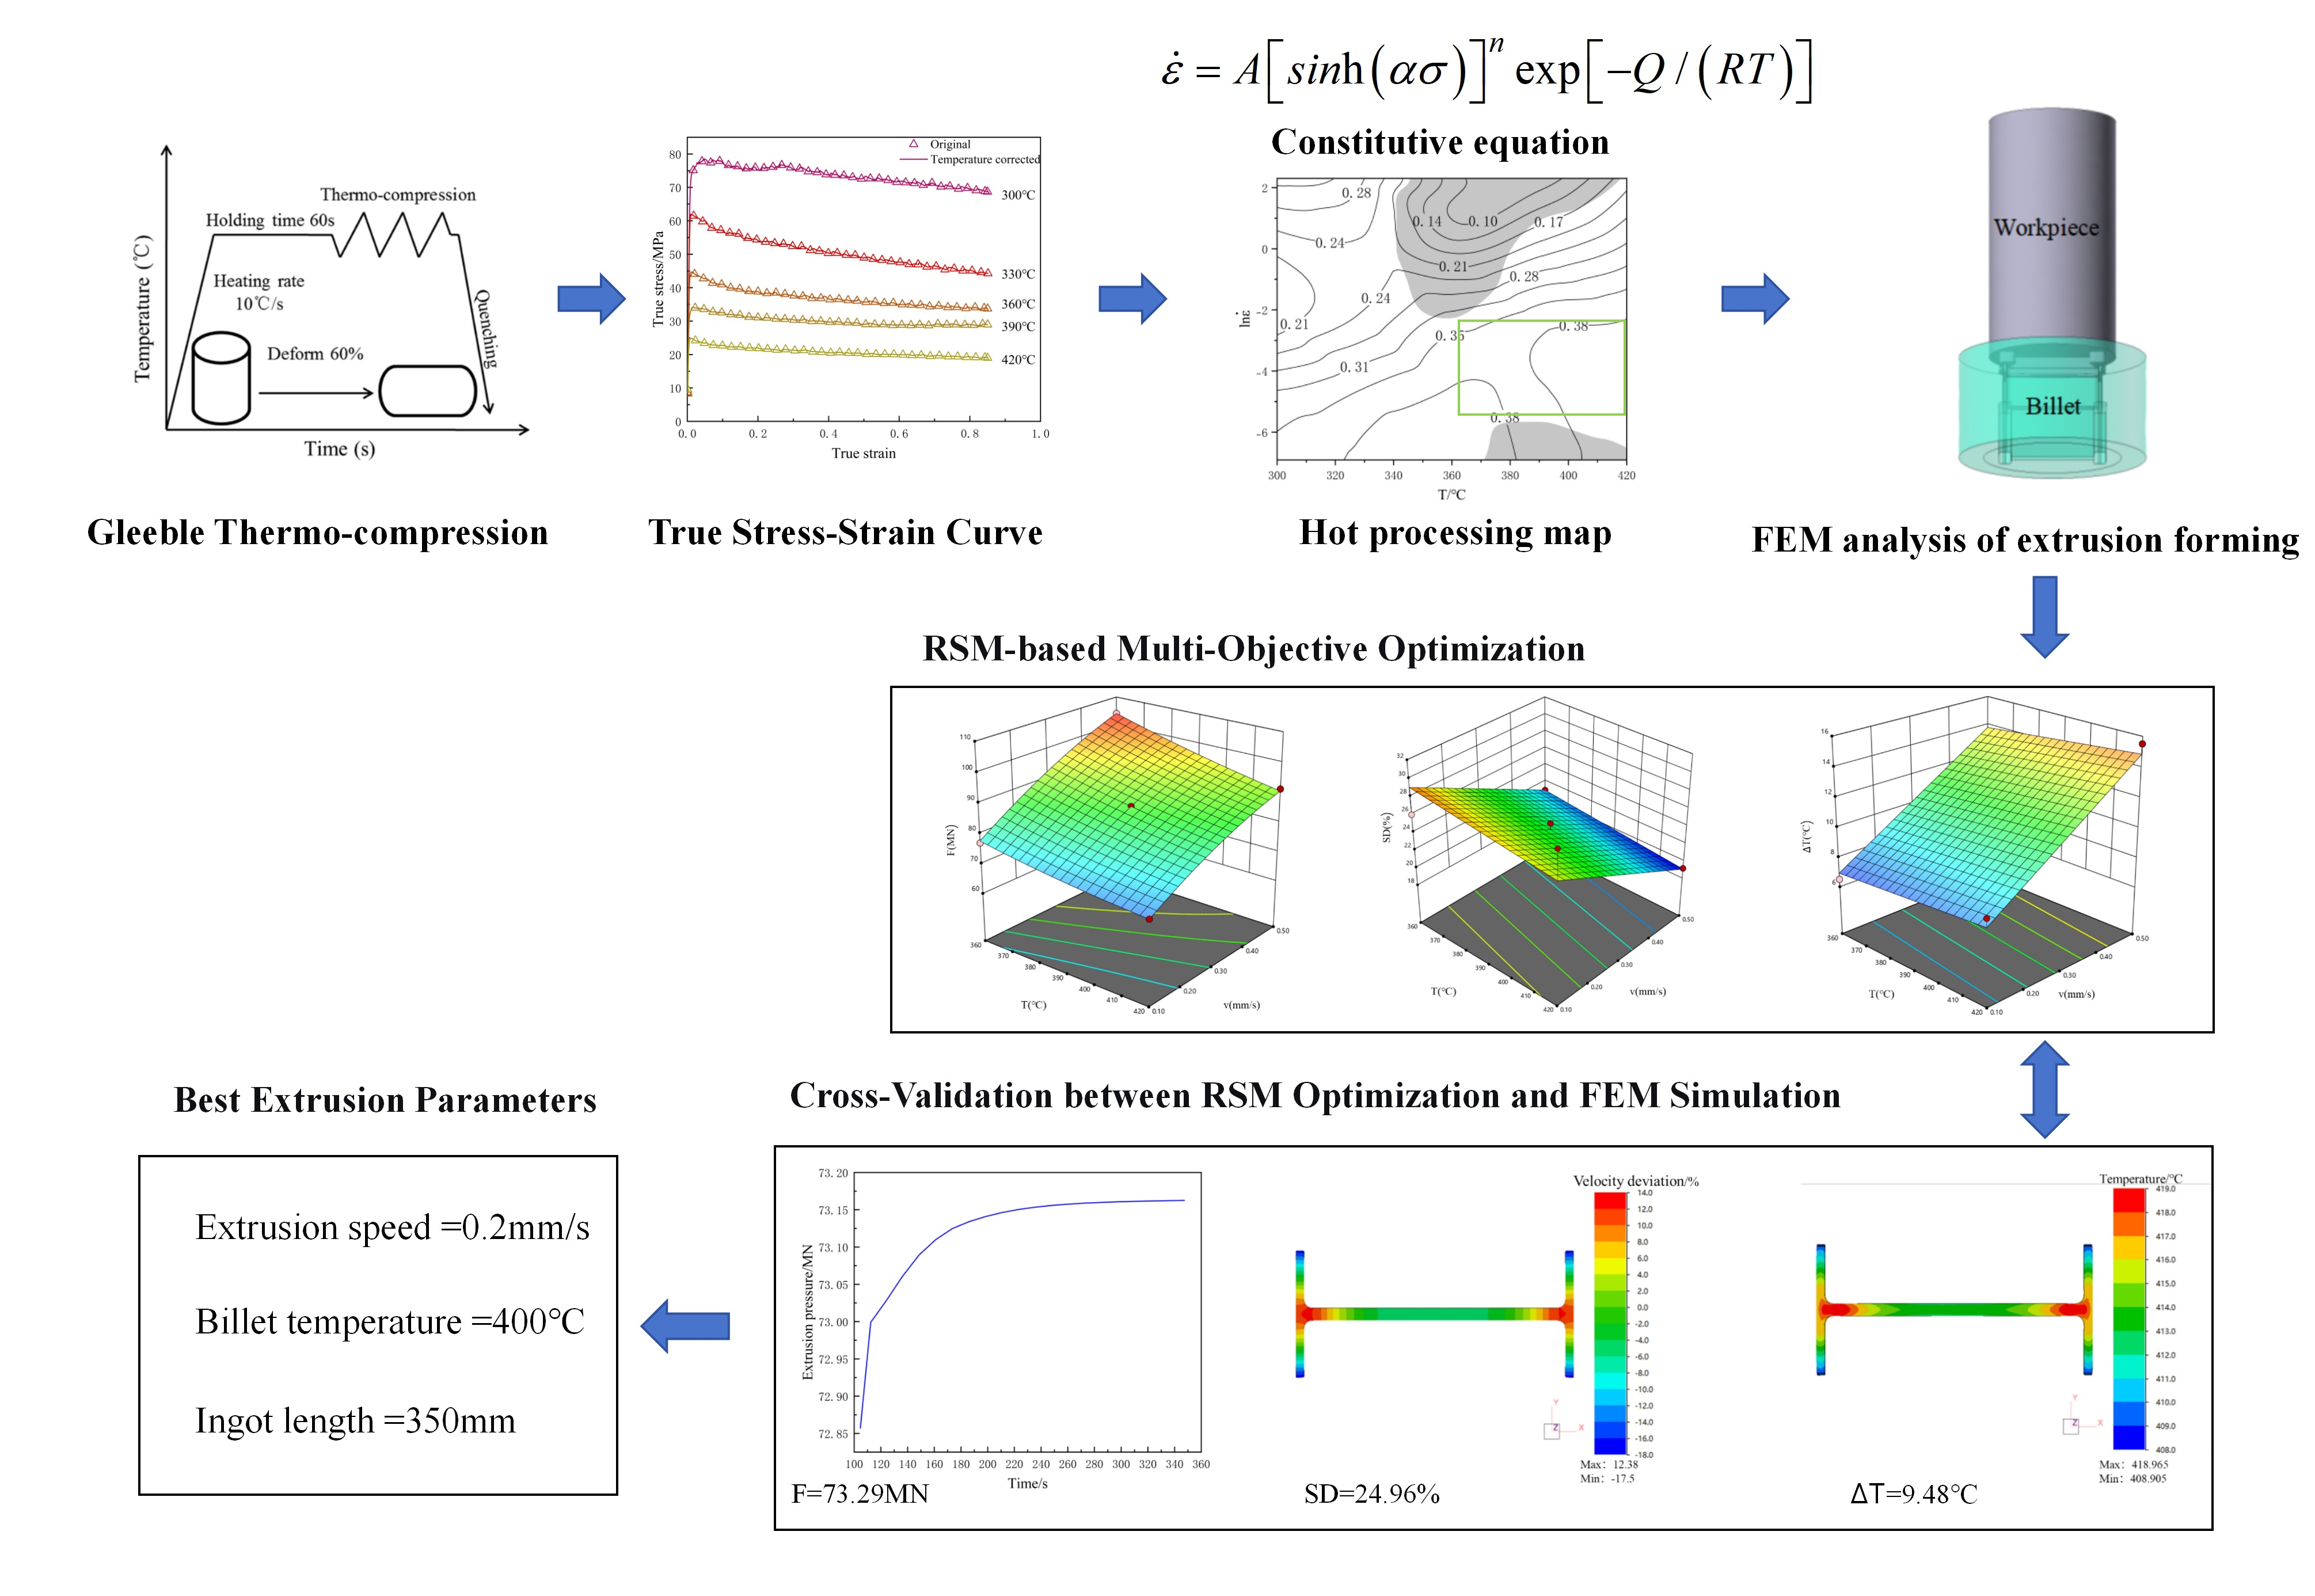
Through multi-objective optimization of the extrusion load for aluminum alloy profiles using response surface methodology (RSM), the optimal parameters were determined: a billet temperature of 400 °C, an extrusion speed of 0.20 mm/s, and an ingot length of 350 mm. Under these conditions, the extrusion load, the profile velocity deviation difference (VDD), and the cross-sectional temperature difference in the extruded profile all reached relatively minimum values. The predicted extrusion load at this point is 73.29 MN, with a VDD of 24.96% and a cross-sectional temperature difference of 9.48 °C.
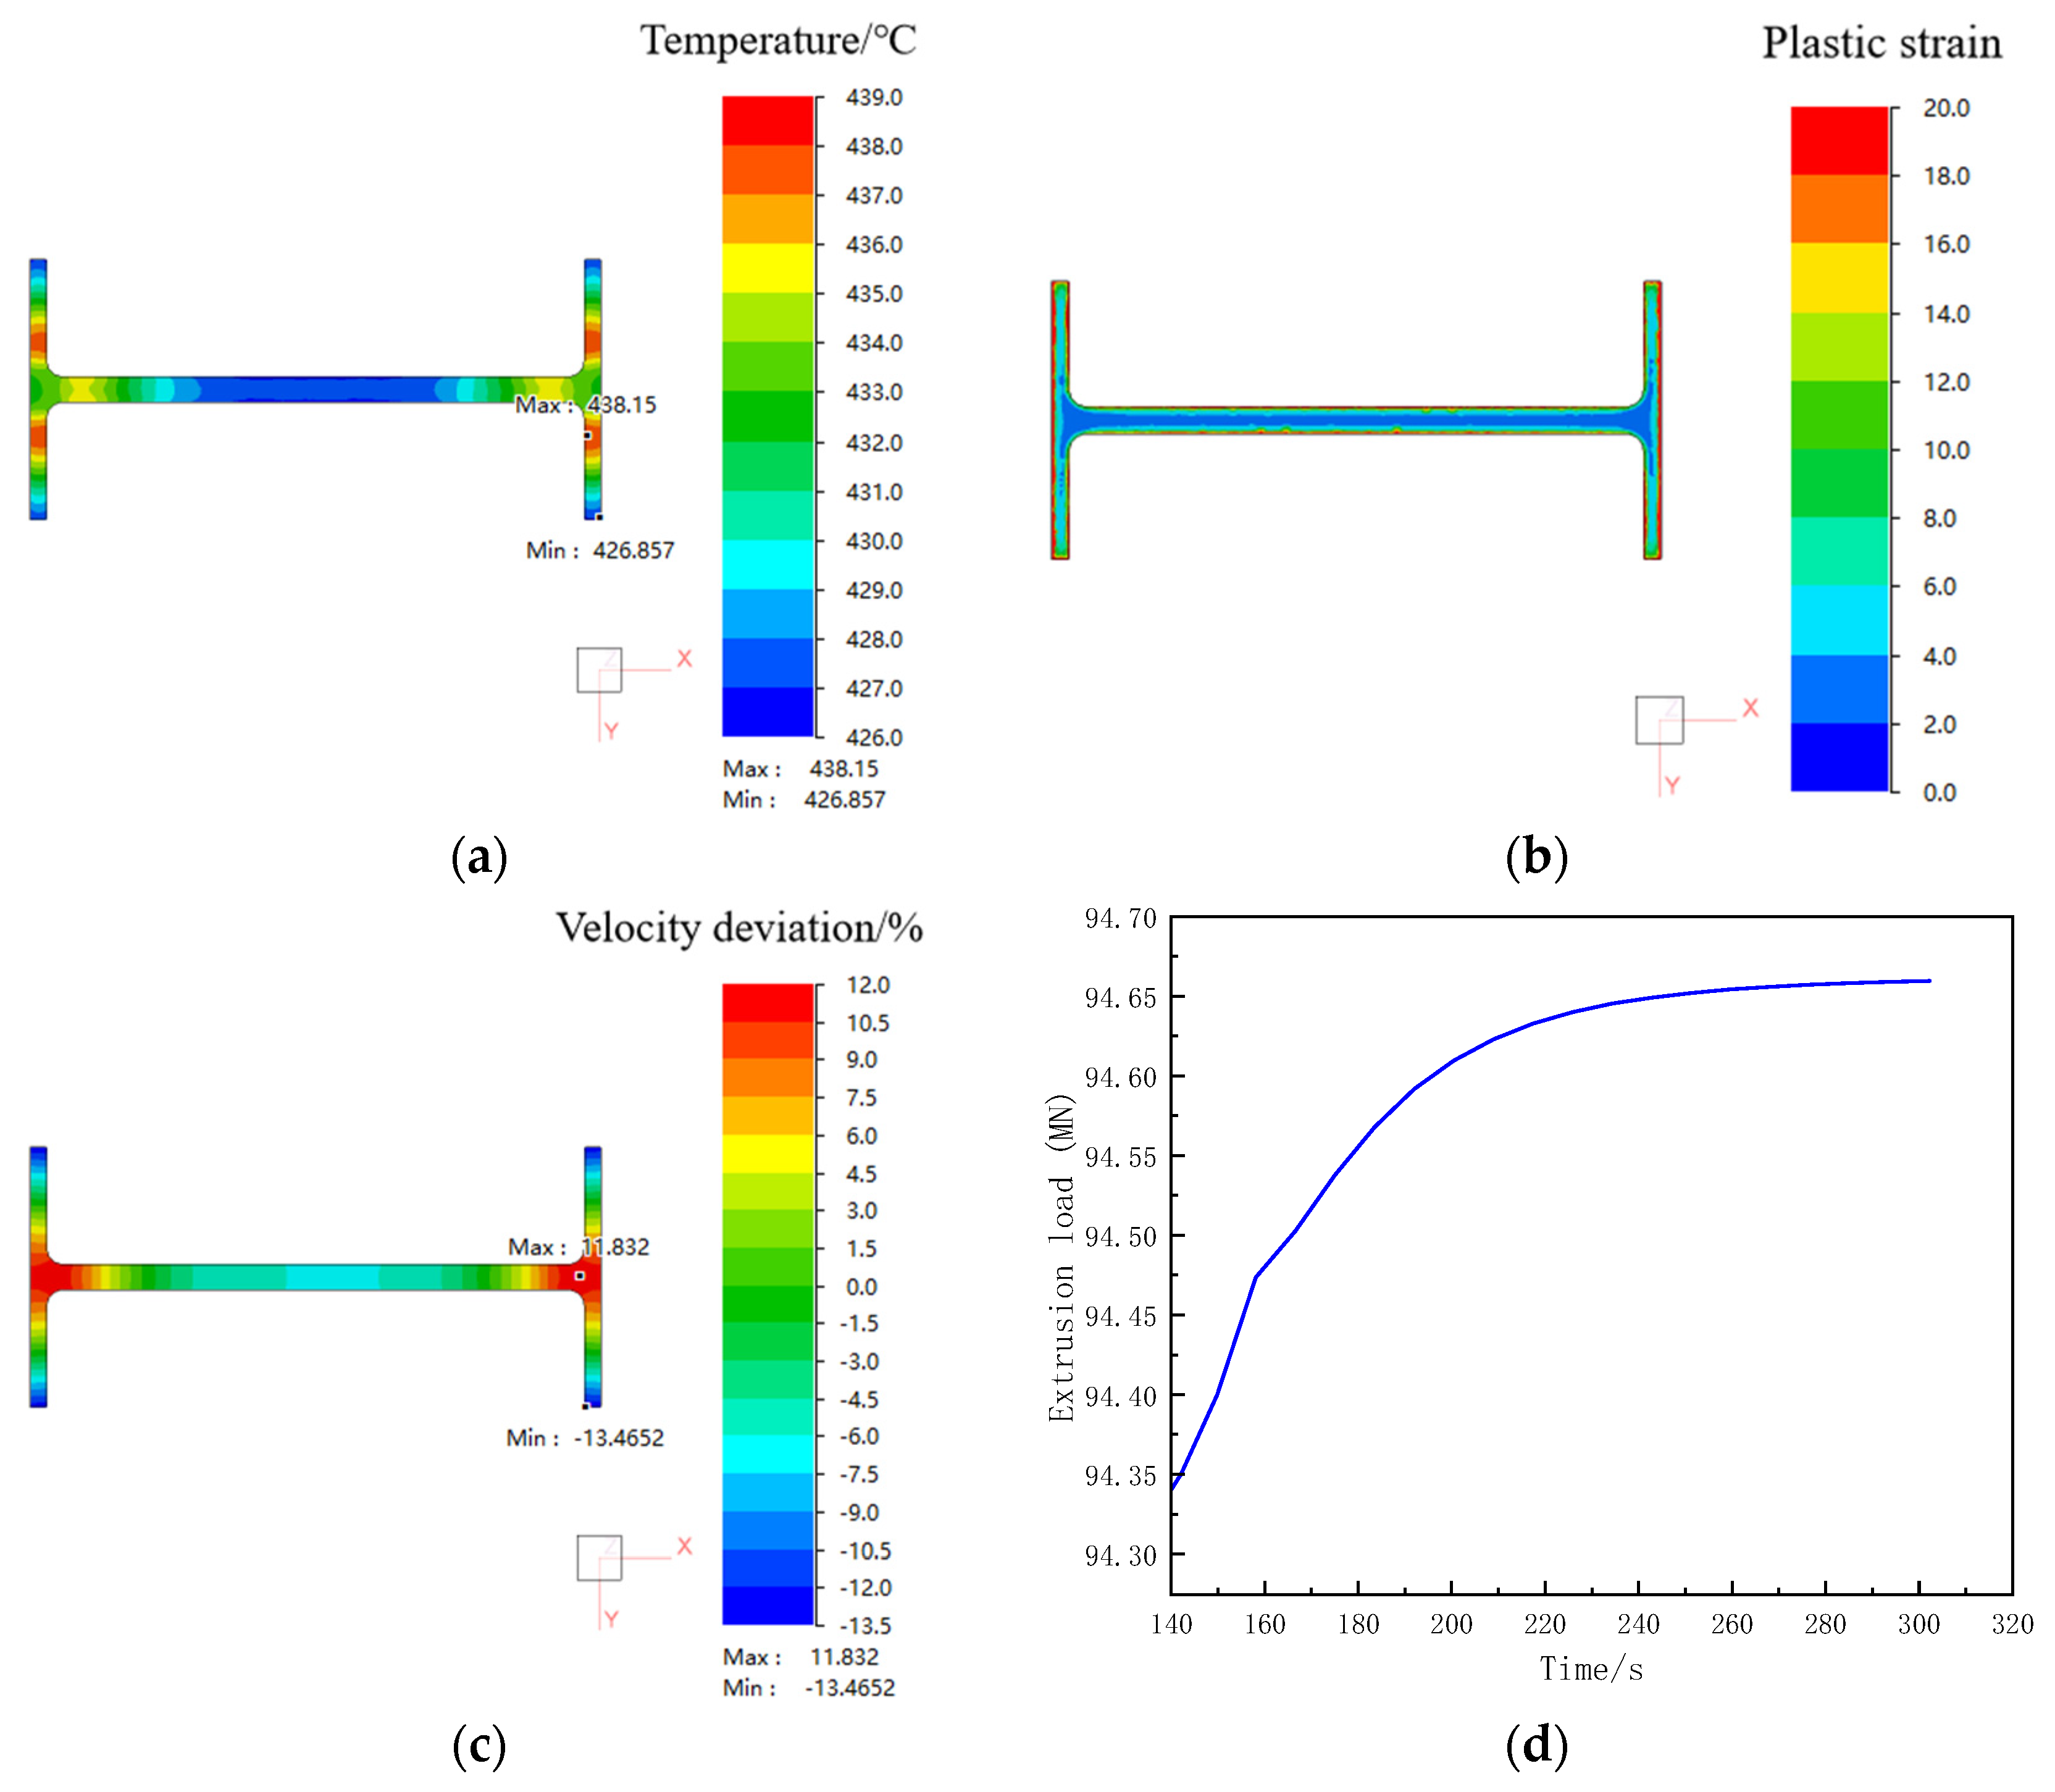
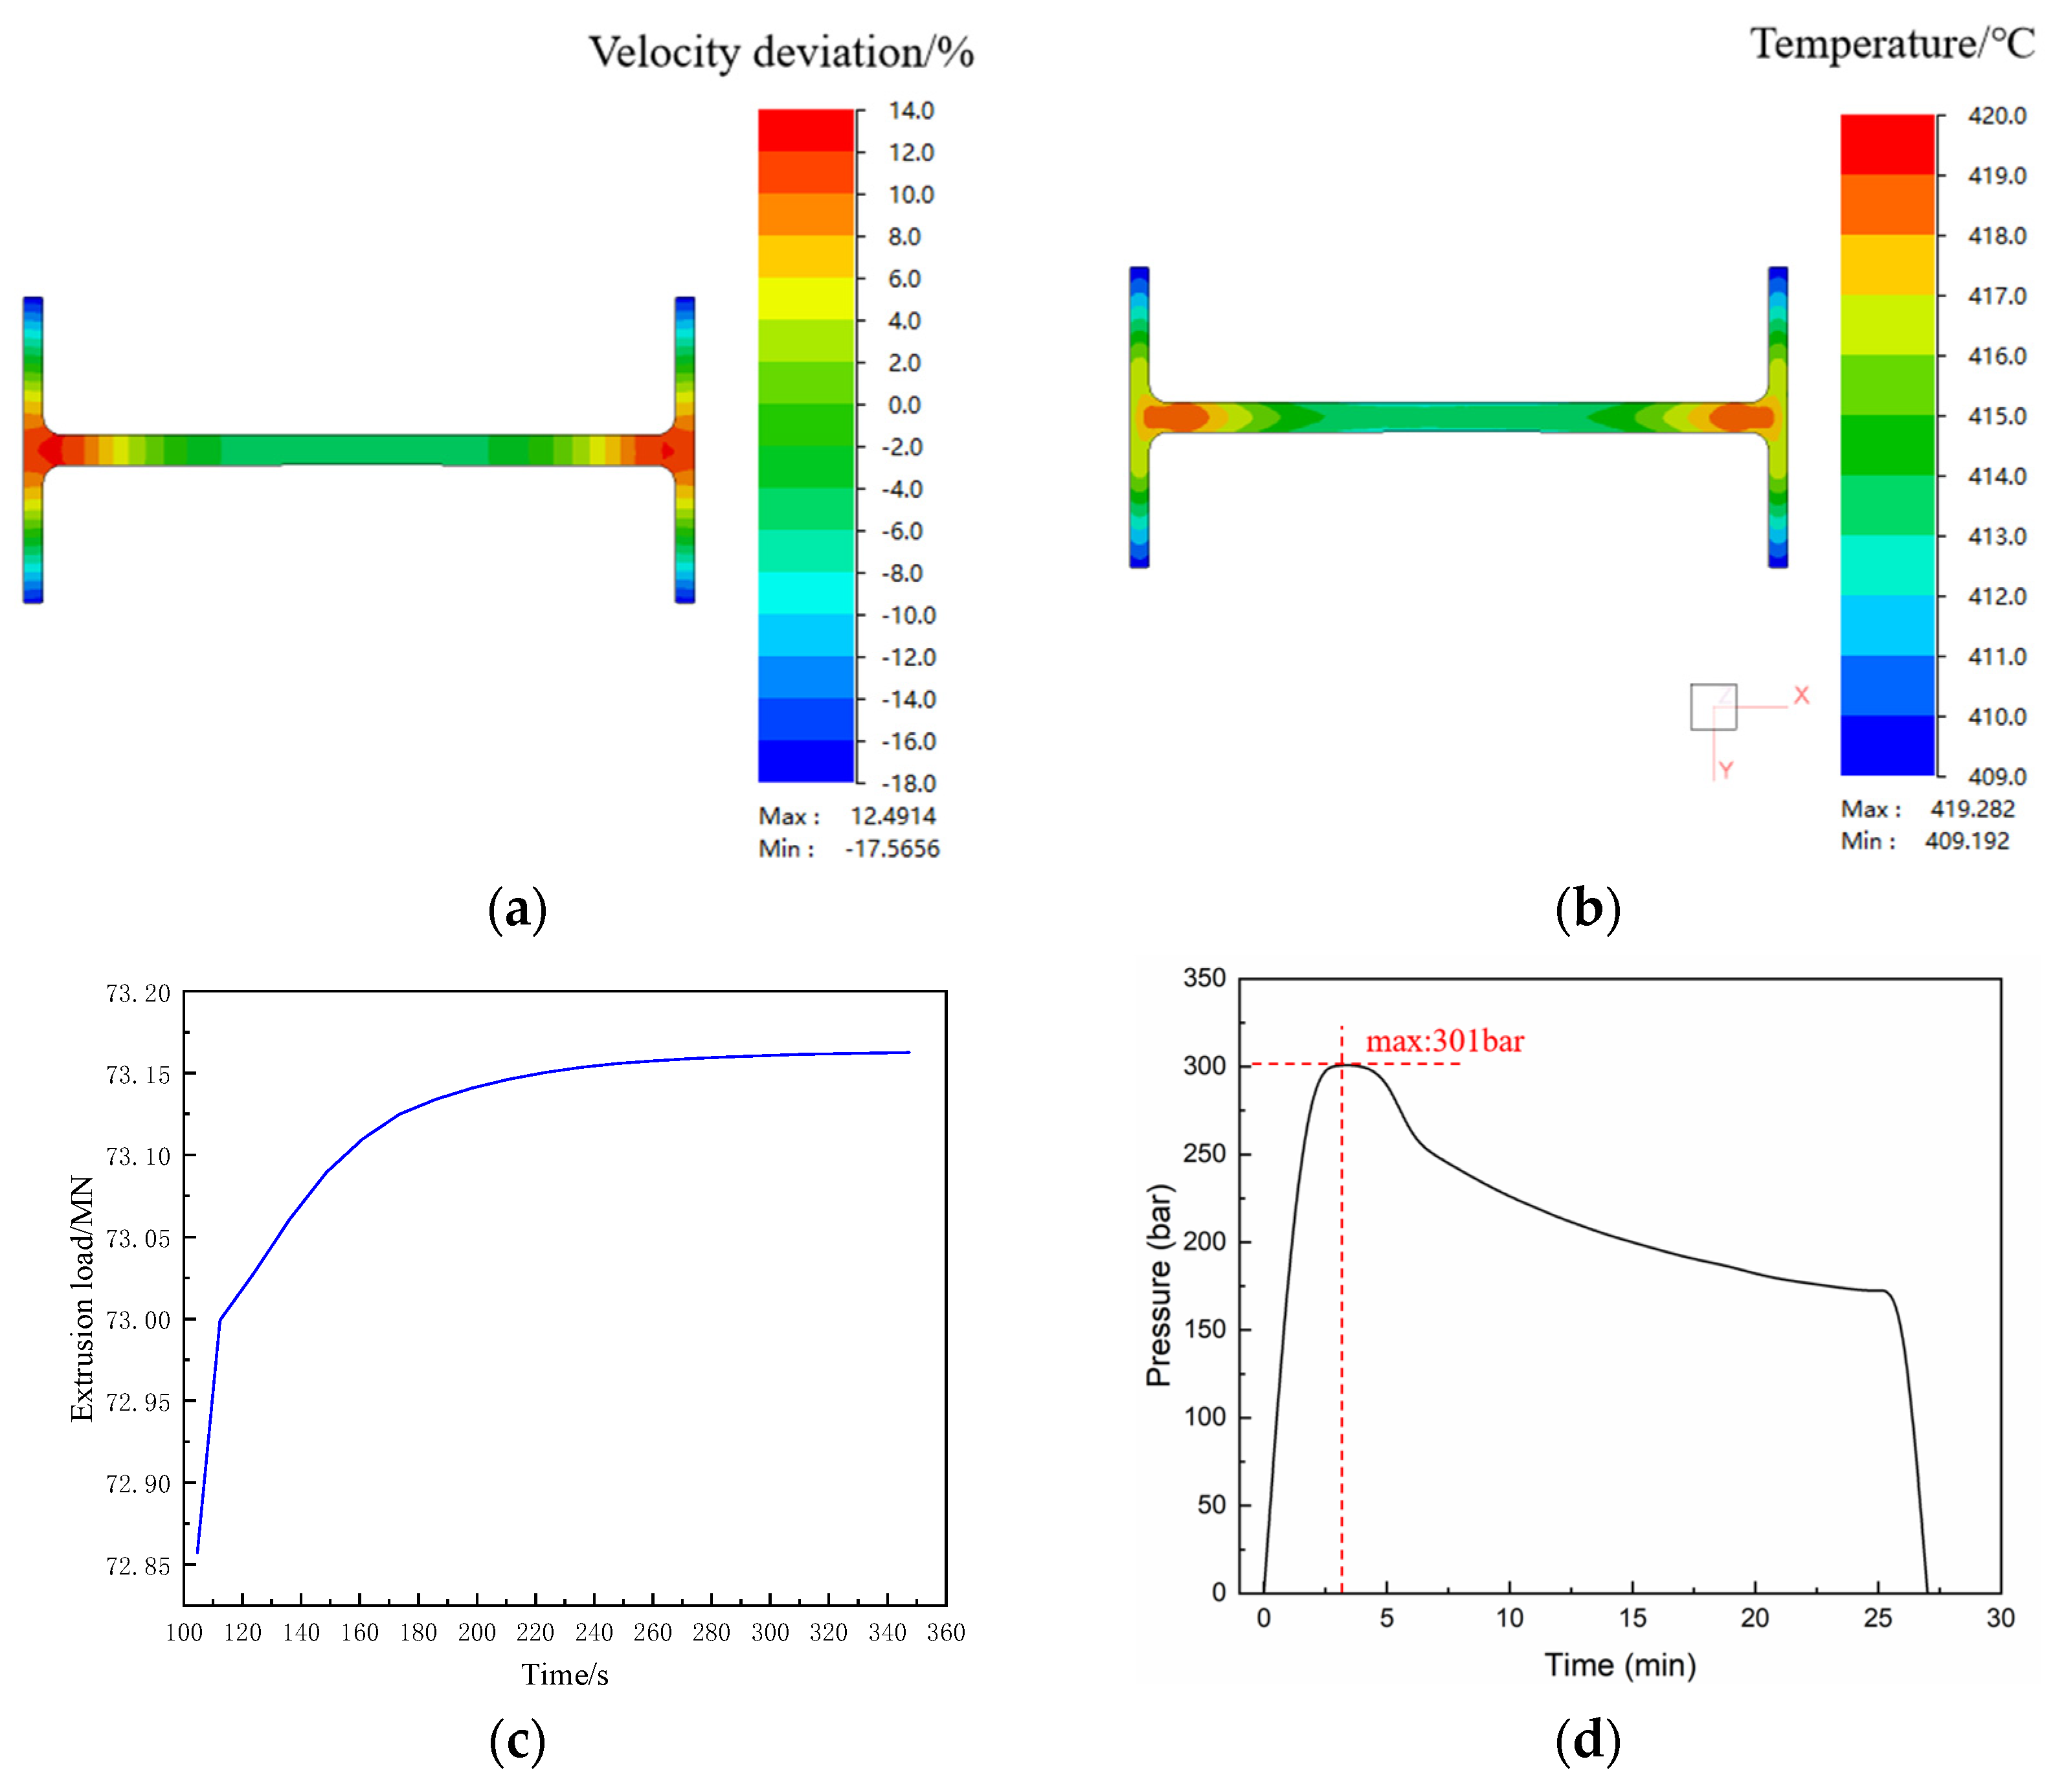
Figure 24 presents the simulation results of the optimized extrusion process parameters based on the RSM model. The optimized parameters yield a VDD of 29.88%, an extrusion load of 73.16 MN, and a cross-sectional temperature difference of 10.06 °C. Notably, the error between the simulated and predicted extrusion load is less than 1%, and the error for the cross-sectional temperature difference is less than 6%, further confirming the significance and reliability of the response surface model. Based on the aforementioned optimization results, a practical extrusion test of the profile was carried out. The extrusion equipment used was an 80 MN extrusion press, with a rated working oil pressure of 320 bar.
Figure 24d shows that the actual breakthrough pressure during extrusion was 301 bar. After a proportional calculation, the actual breakthrough extrusion load was 75.25 MN, while the simulated prediction was 73.29 MN. The prediction error is less than 5%, indicating that the finite element simulation results are reliable.
The use of optimized process parameters significantly reduces the extrusion load, which facilitates the engineering application of high-magnesium low-density aluminum alloy profiles. However, the error between the simulated and predicted VDD is less than 17%, indicating a relatively large discrepancy. In the model, only the extrusion speed is identified as a significant term affecting VDD, while other parameters show no significance. This suggests that improving the uniformity of the extrusion flow velocity requires optimization of the die structure, as the extrusion process parameters have limited influence on the uniformity of extrusion flow velocity.